Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

博客

  • Rebar Handling Crane Systems

    Rebar Handling Crane Systems

    Rebar Handling Crane Systems

    Henan Mine Crane · Engineered Long-Steel Transfer Systems

    Rebar Handling Crane Systems

    Overhead cranes engineered for receiving, transferring, stacking, retrieving and dispatching straight rebar bundles, reinforcing steel bars and compatible long-steel products.

    Henan Mine Crane configures every rebar handling crane from the declared bar material, bundle length and diameter, maximum gross suspended load, bundle condition, surface coating, storage layout, cycle rate, runway limits and required control level. Available concepts include fixed or rotating electromagnetic beams, hook cranes with multi-point spreader beams, purpose-designed clamps and coordinated automatic warehouse systems.

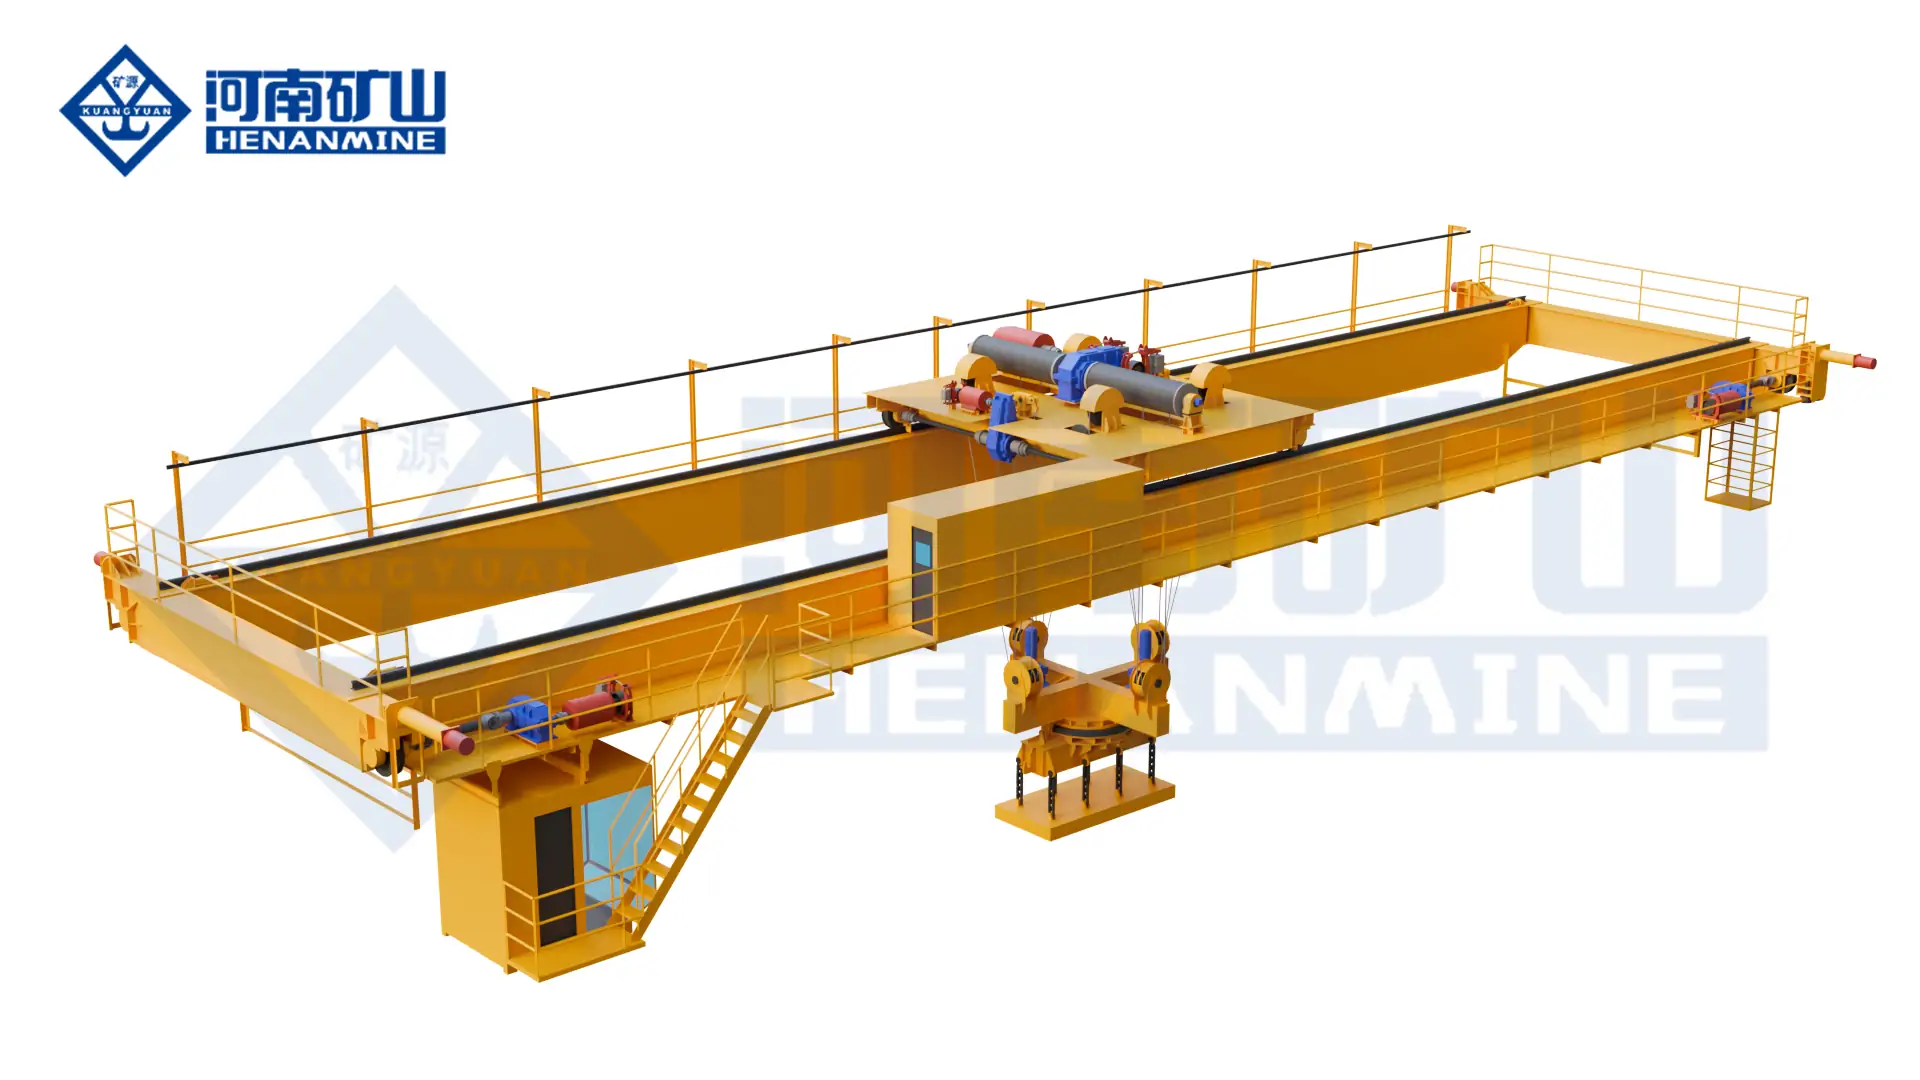
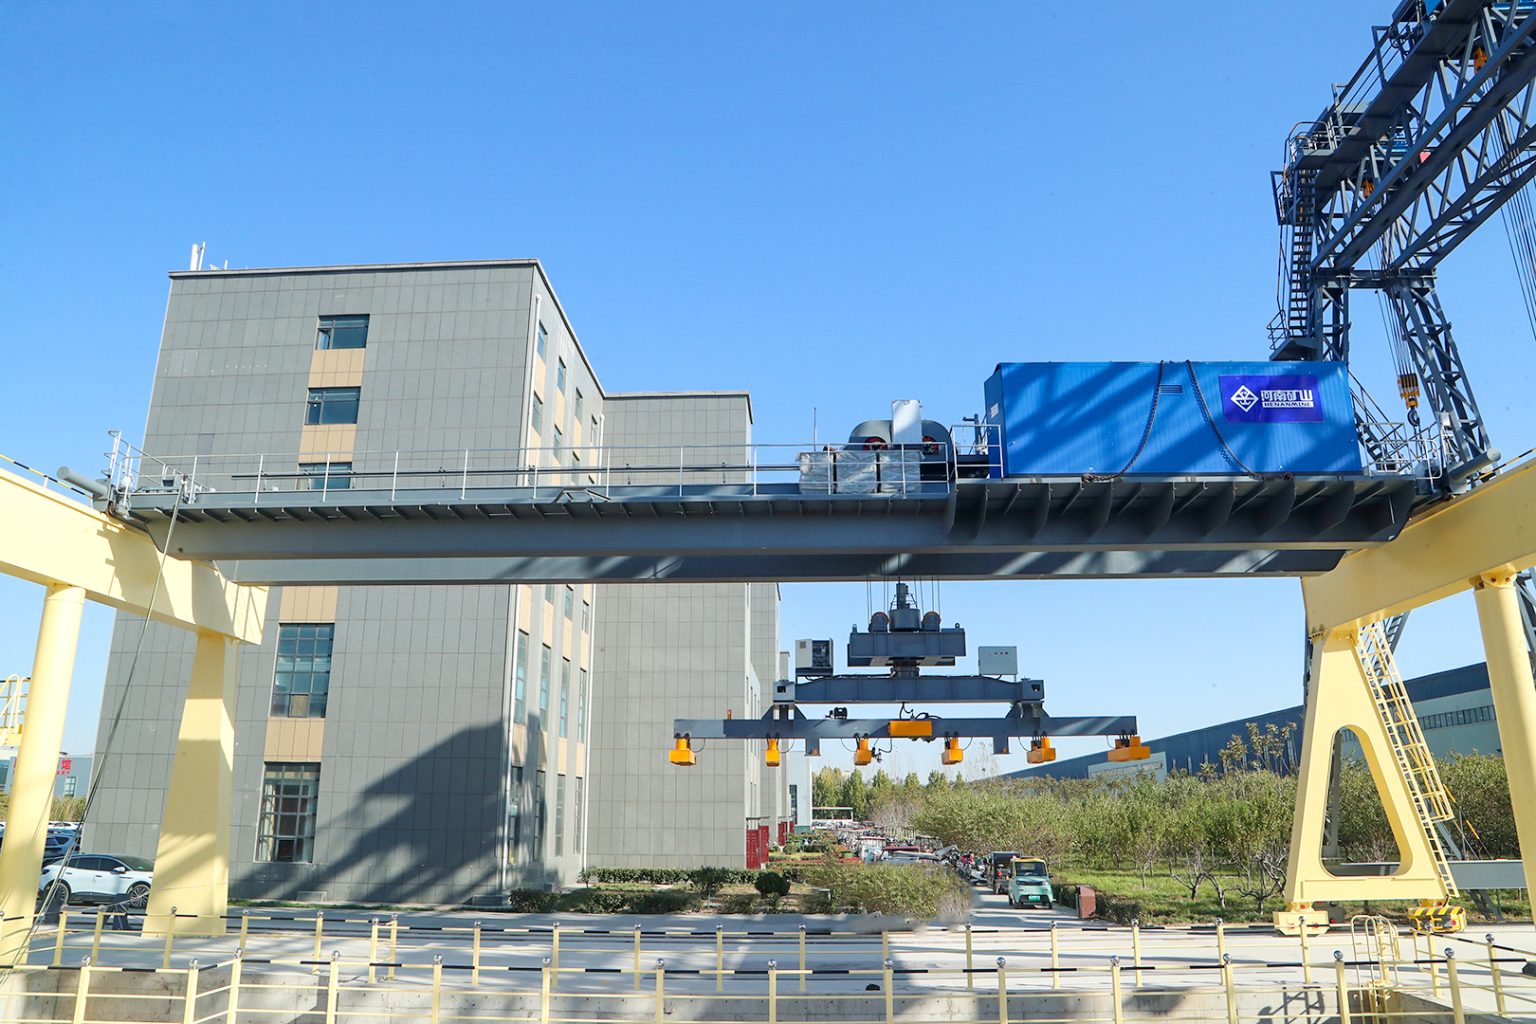
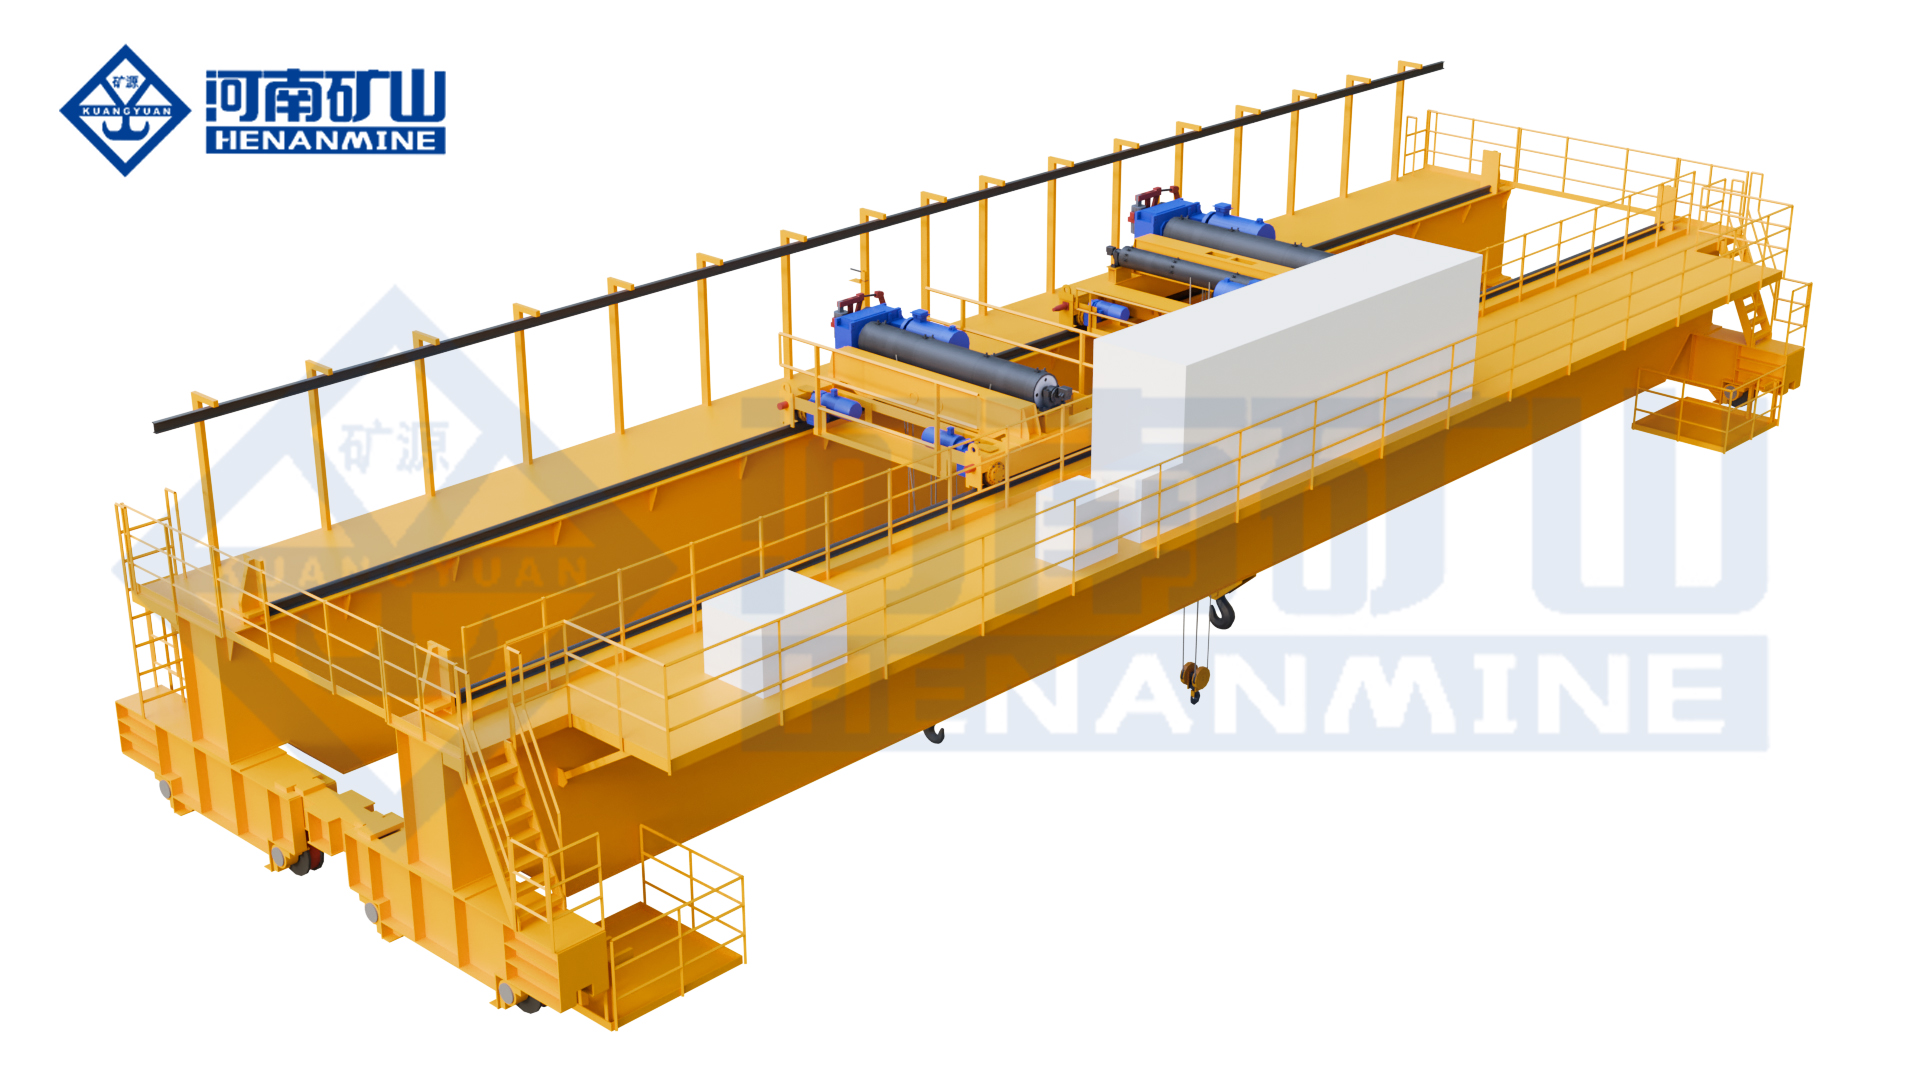
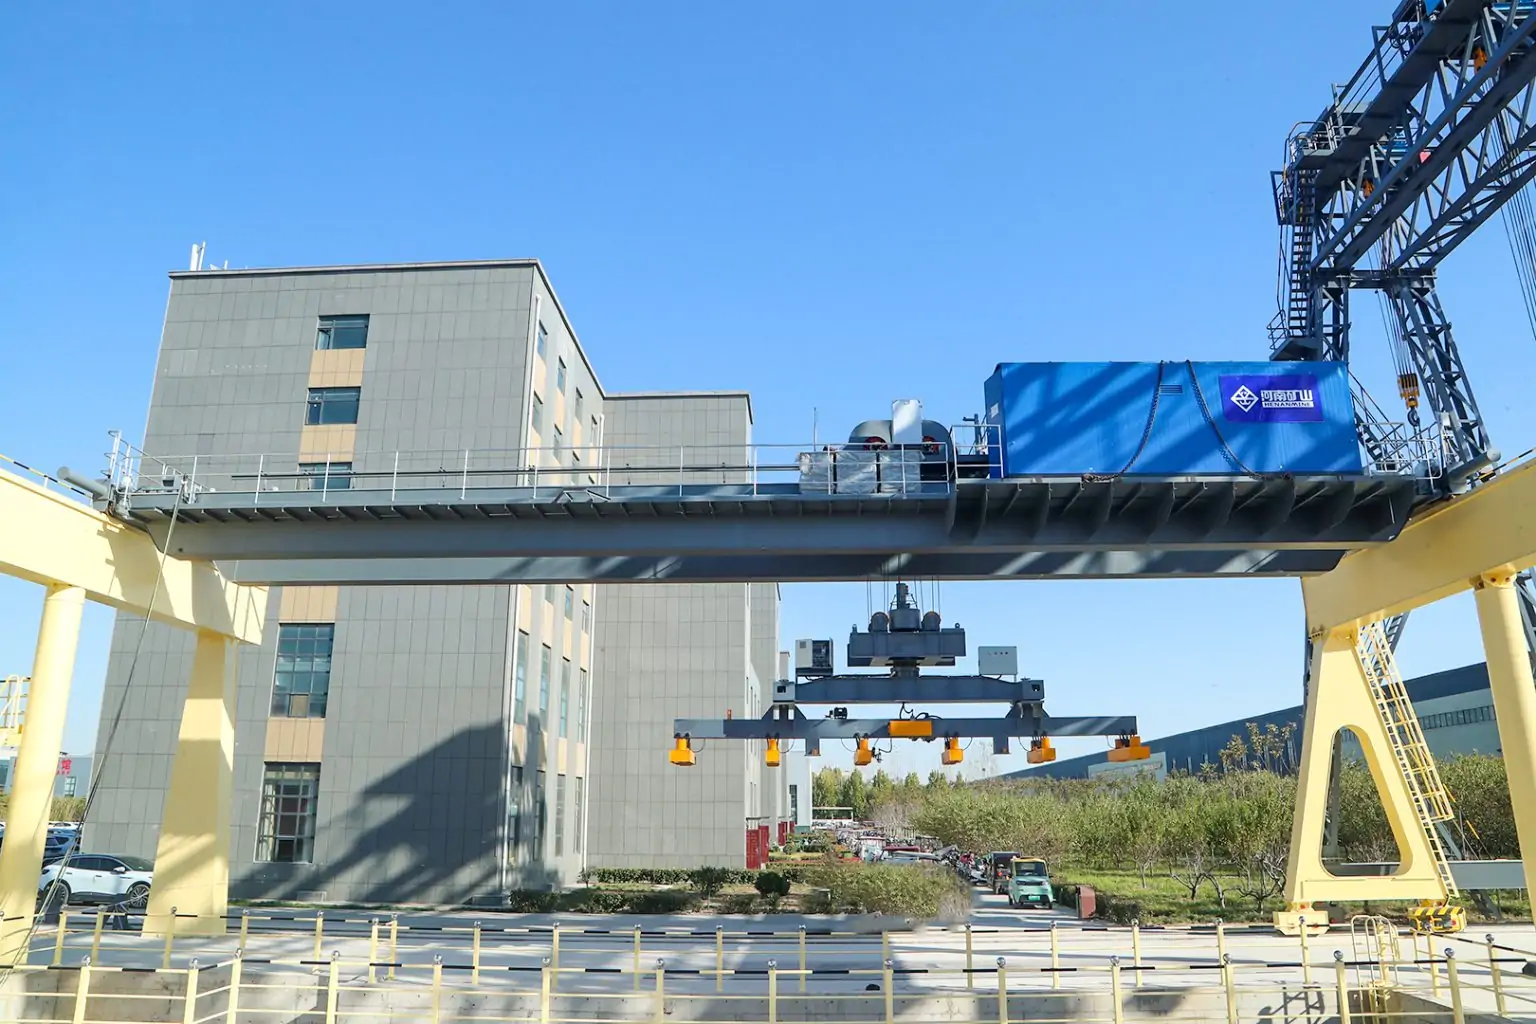
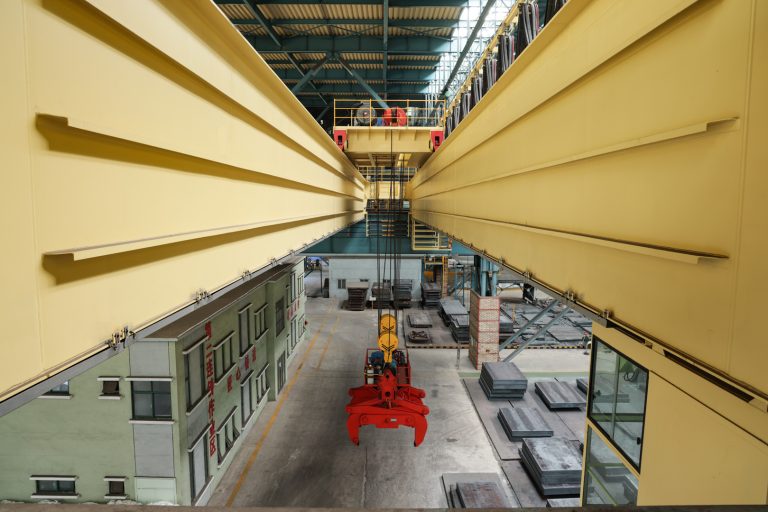
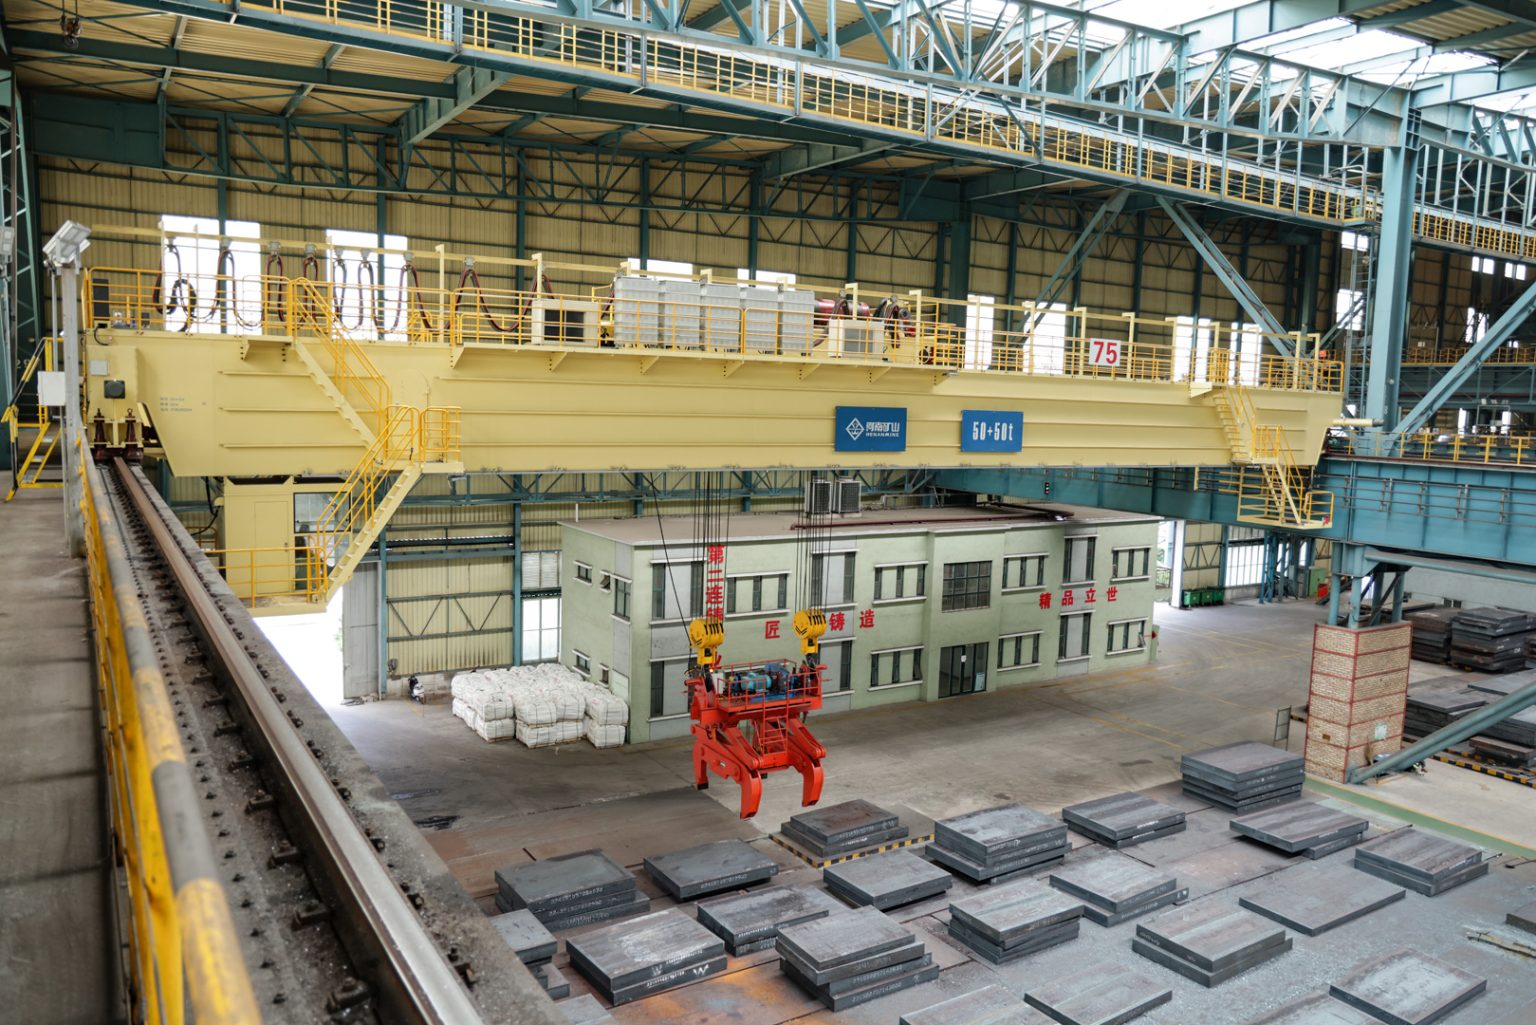
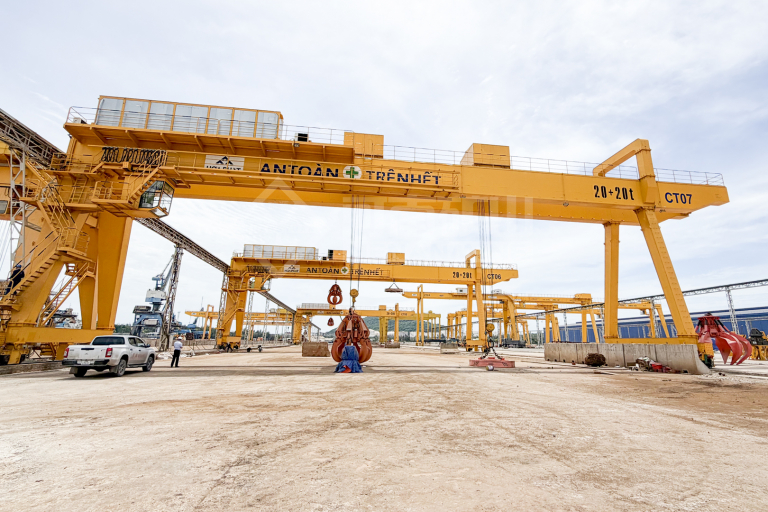
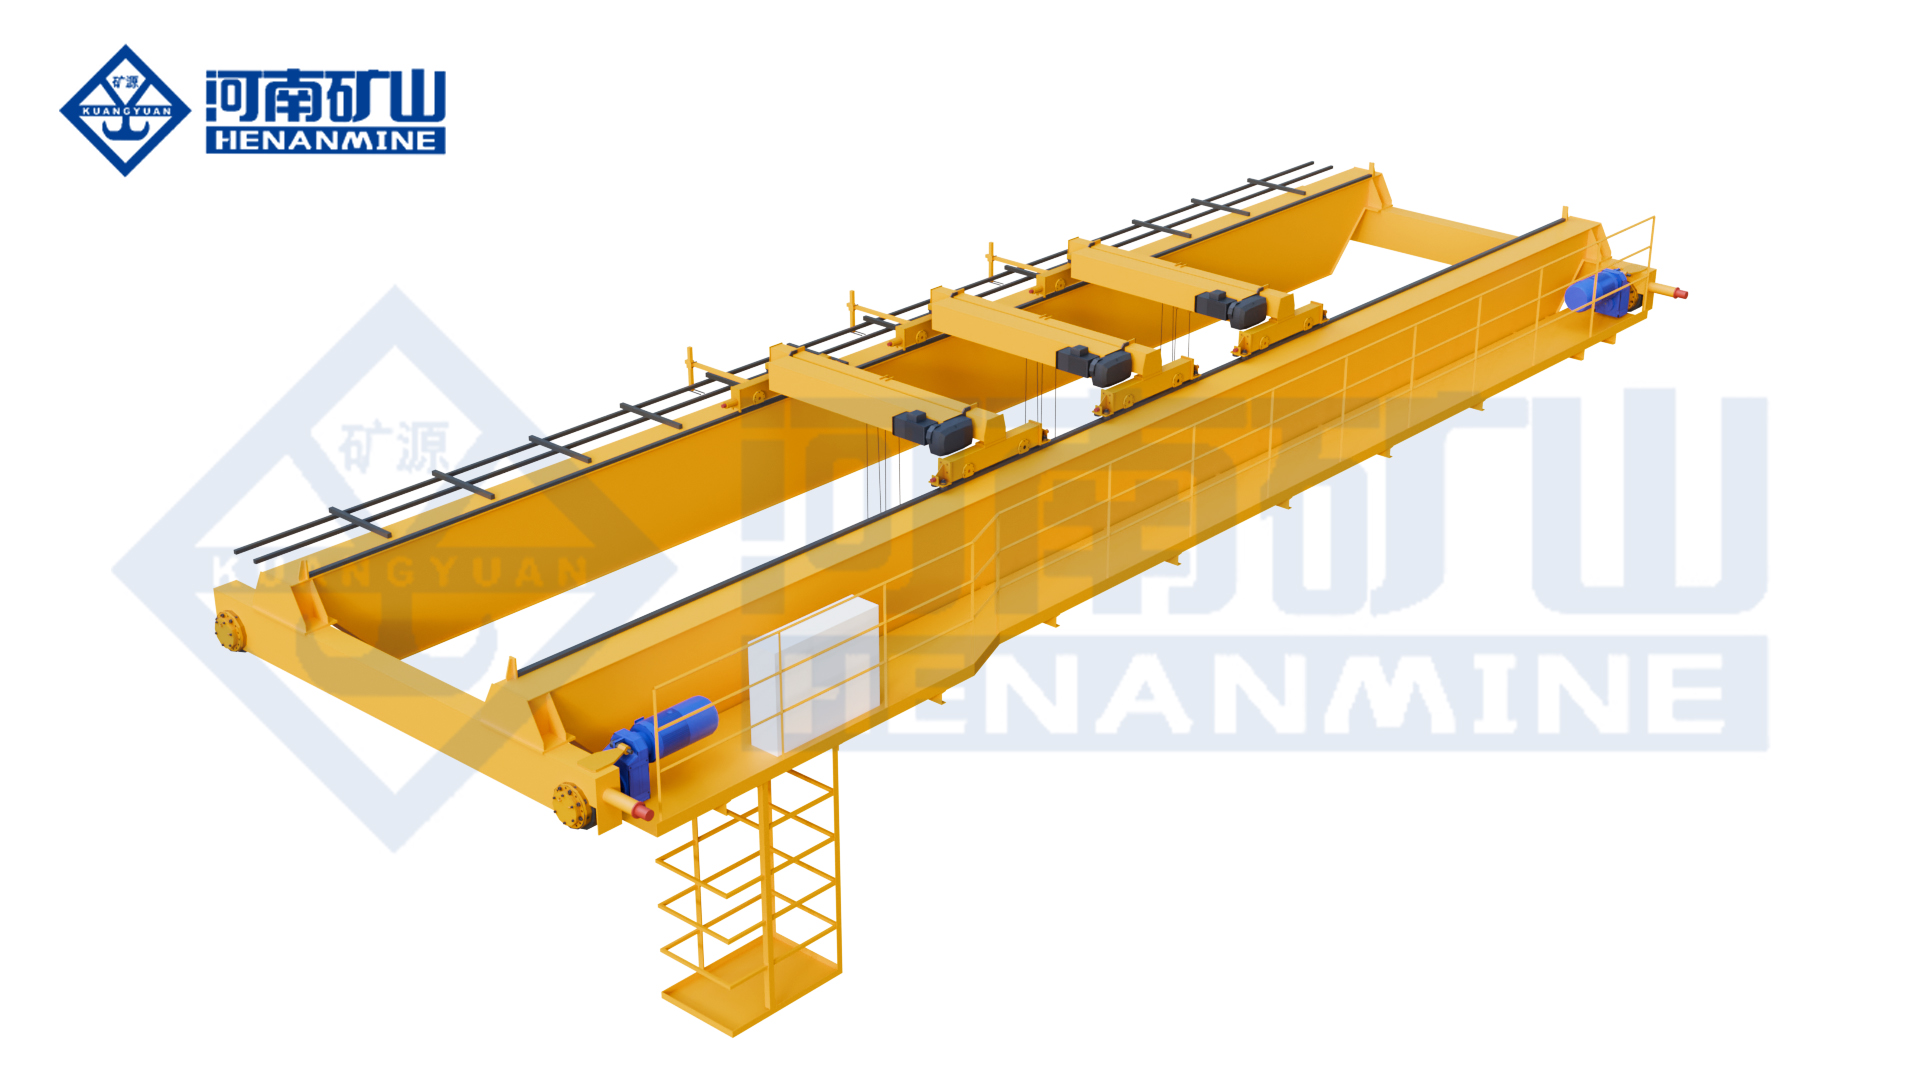
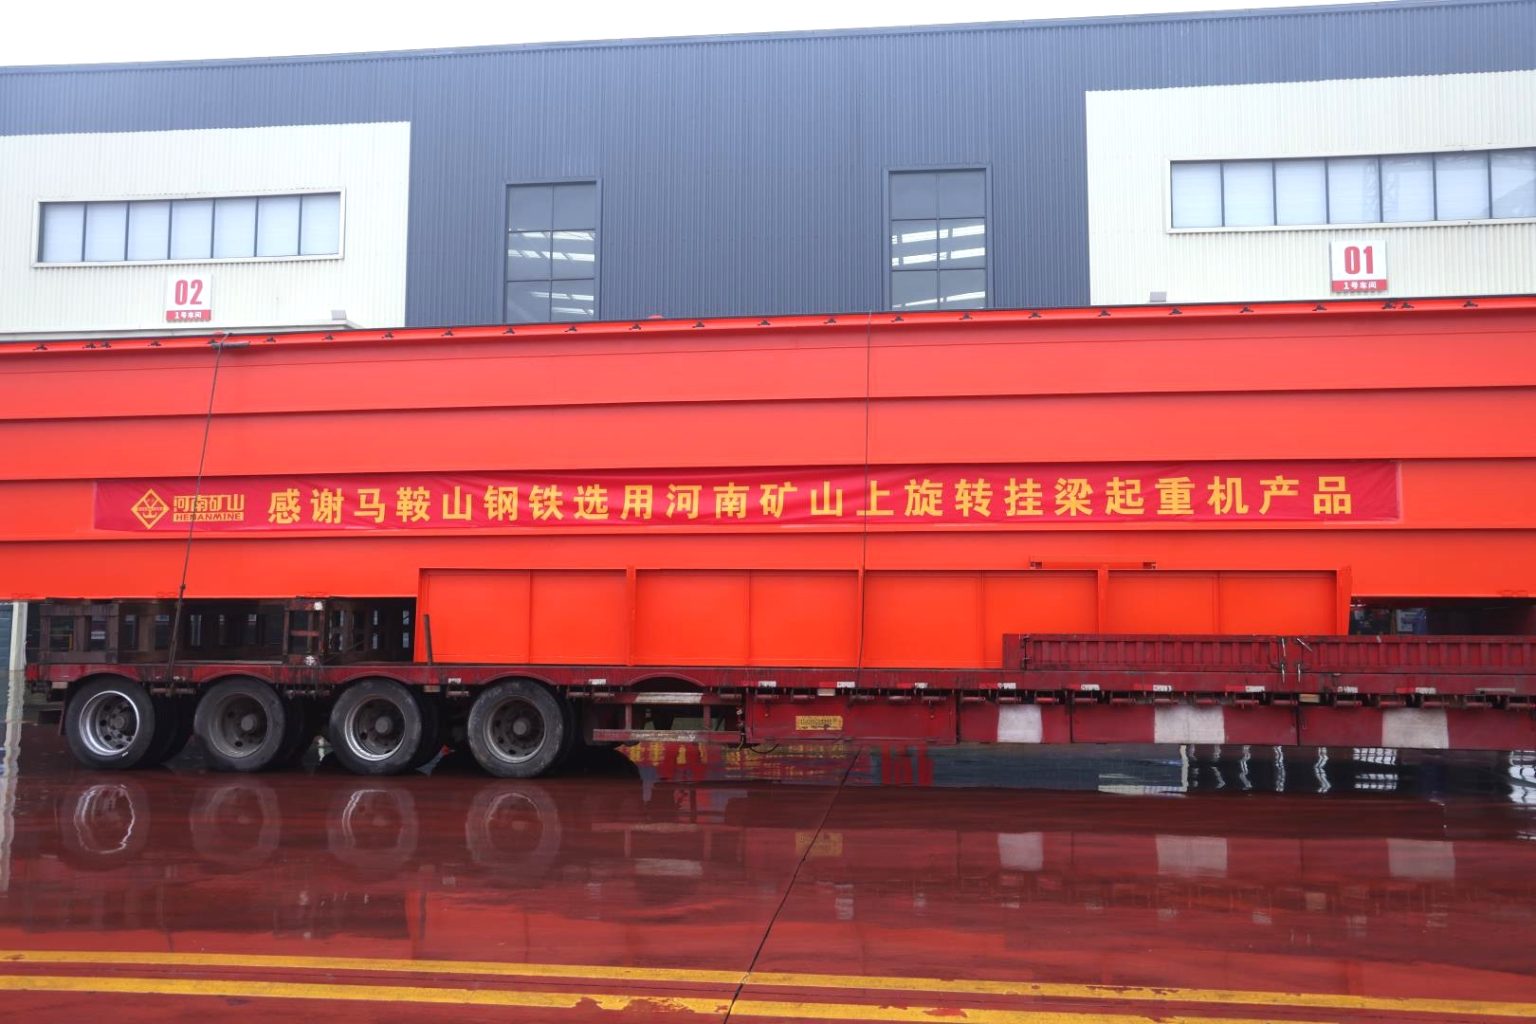
    rotating electromagnetic beam overhead crane platform for rebar and long steel handling
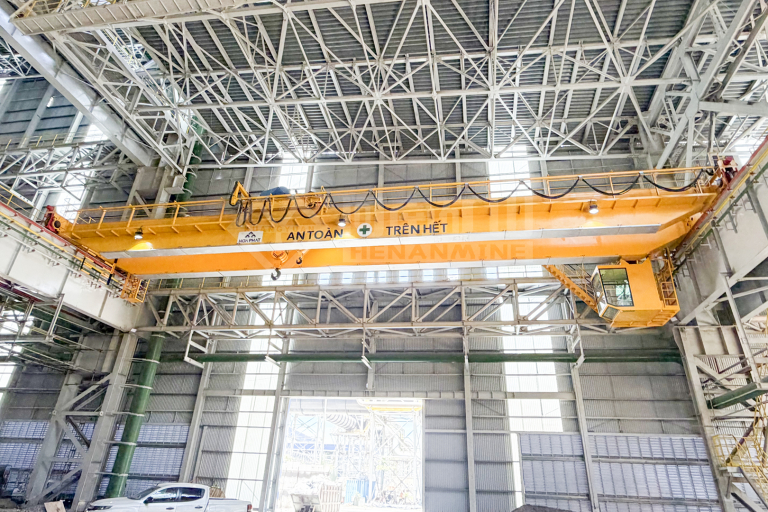
    A double-girder crane can carry a fixed, rotating or telescopic beam with magnets or mechanical lifting points selected for the confirmed rebar bundle matrix.

    PRIMARY ARCHITECTURE

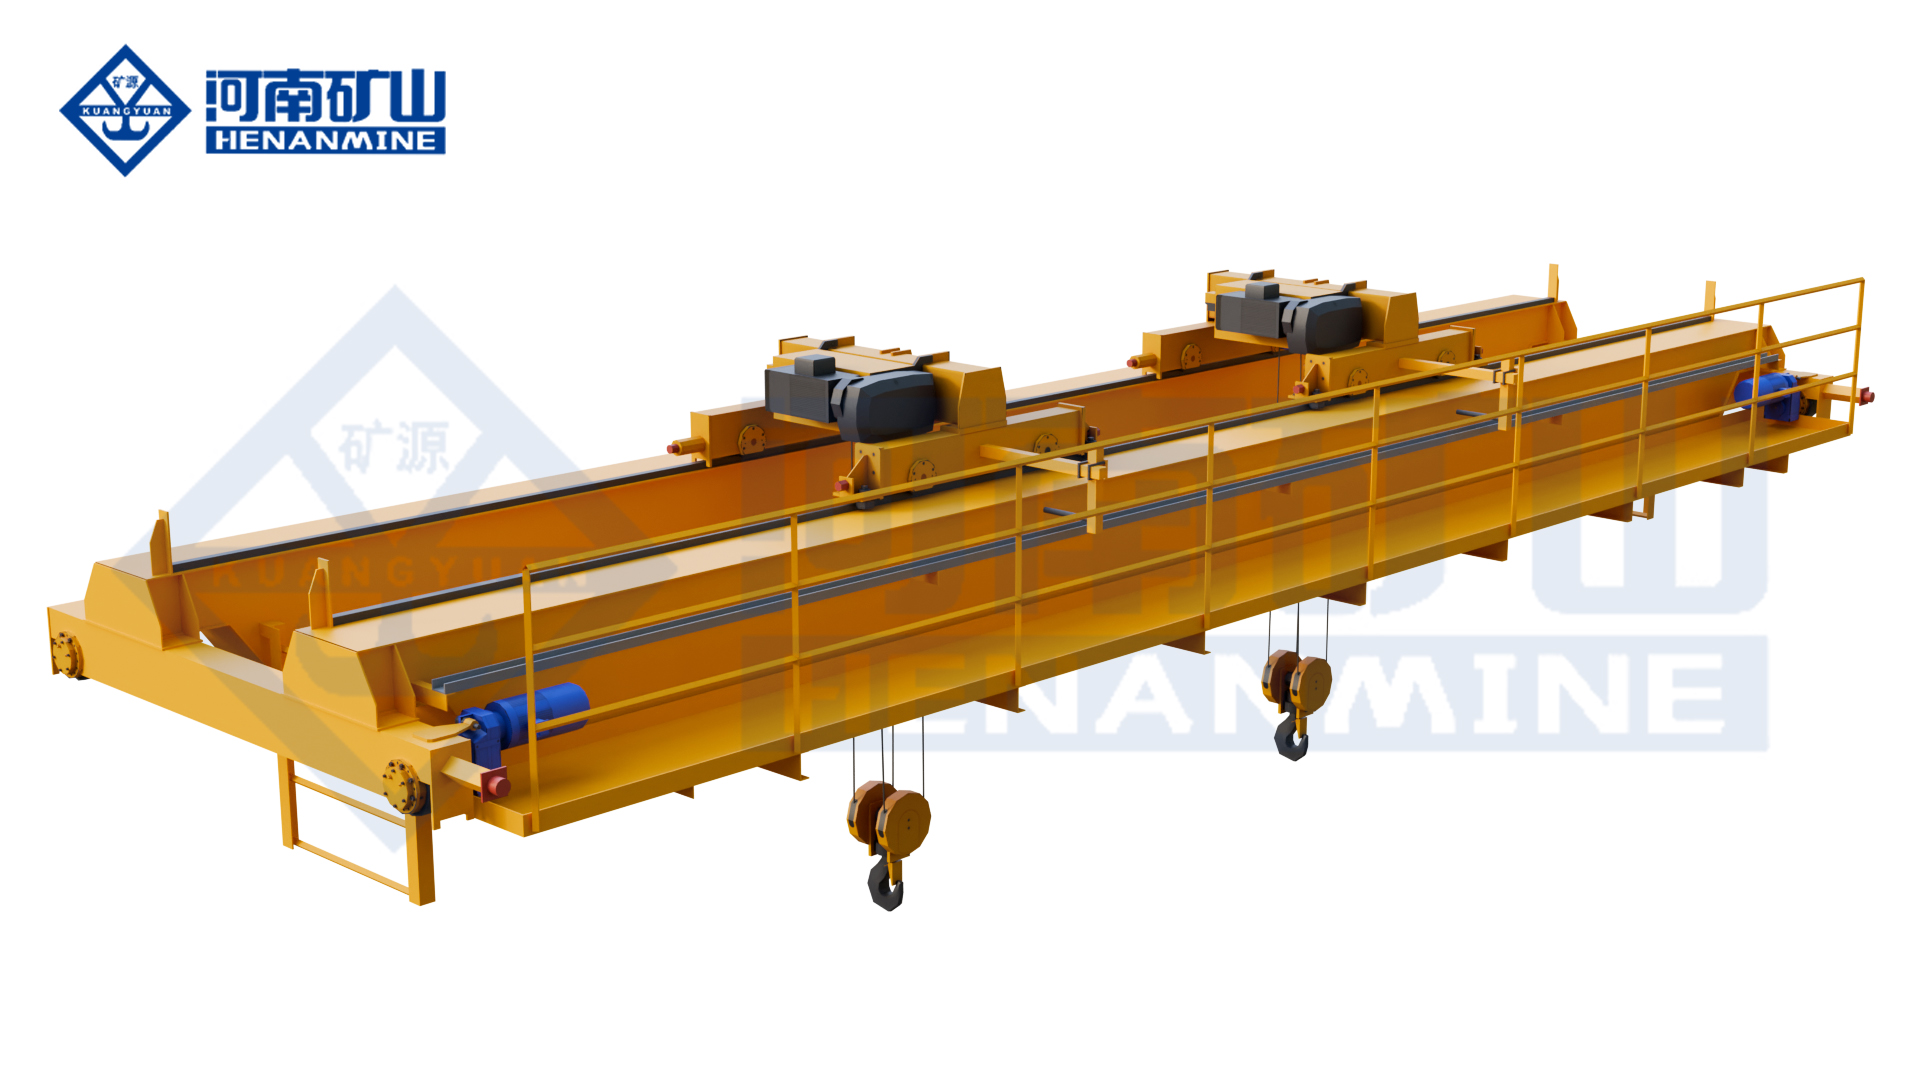
    Top-Running Double Girder

    LOAD FORM

    Straight Rebar Bundles & Long Steel

    LIFTING SYSTEMS

    Magnet, Spreader, Sling or Clamp

    CONTROL OPTIONS

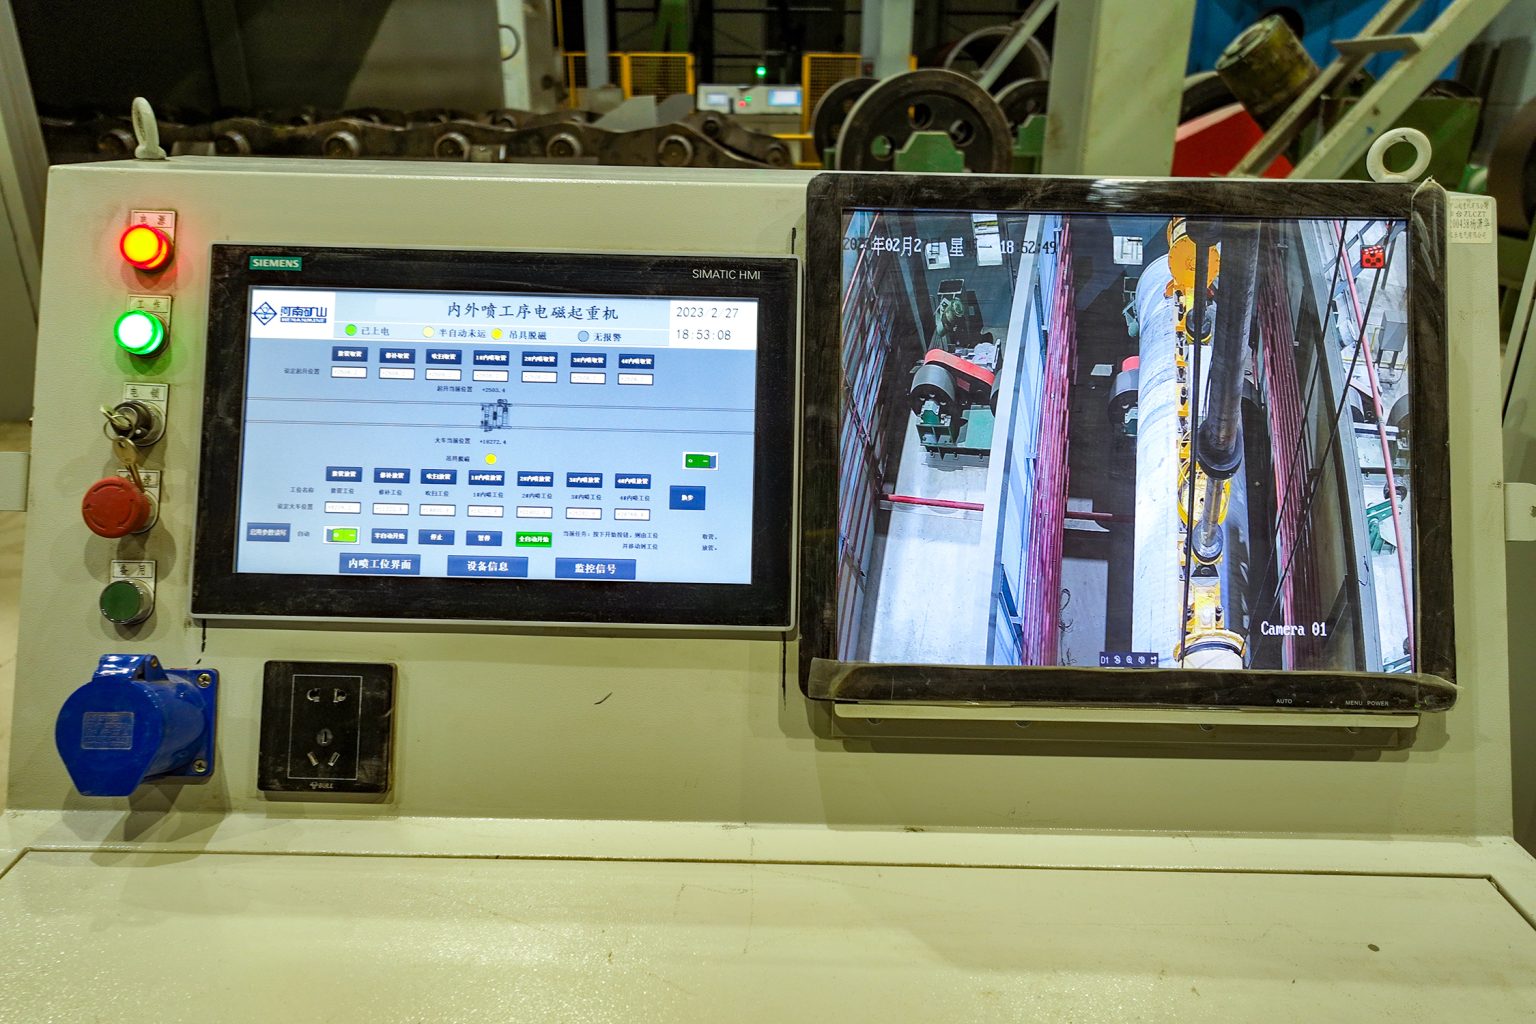
    Cabin, Radio, PLC & Automation

    What Is a Rebar Handling Crane?

    A rebar handling crane is an overhead process crane equipped to lift and position straight reinforcing bars or bundled long steel. It supports rolling-mill finishing bays, rebar production lines, steel service centers, reinforcement fabrication plants, distribution warehouses, truck-loading areas and construction-material logistics facilities.

    Rebar creates a different lifting problem from compact unit loads. A bundle may be 6–18 m long, flexible relative to its length and secured by multiple ties. Its center of gravity can shift when bars are unequal, loose or partly withdrawn. The lifting system must distribute support along the bundle, maintain orientation, avoid excessive sag and place the material within the available rack, truck or processing-line clearance.

    Magnetic handling is efficient for validated ferromagnetic black rebar, but it is not automatically suitable for every reinforcing product. Steel grade, bar diameter, rib geometry, rust or scale, surface coating, temperature, air gaps, bundle shape and the number of bars retained by each magnet all affect the lifting result. Epoxy-coated, galvanized or stainless reinforcing bar may require a protected mechanical system instead.

    Henan Mine Crane combines the lifting attachment with an electromagnetic hanging crane, electromagnetic bridge crane, double-girder bridge crane or process-duty metallurgical platform according to the approved load and operating route.

    Rebar Handling Crane Applications

    Rolling-Mill Finishing Bay

    Transfer cut-to-length bars from collection beds to inspection, bundling, weighing, storage and dispatch positions.

    Finished-Rebar Warehouse

    Stack, retrieve and sequence bundles by heat, diameter, length, grade, customer order or vehicle-loading plan.

    Rebar Fabrication Plant

    Feed straight bars to cutting and bending equipment and move prepared reinforcement assemblies within defined handling zones.

    Steel Service Center

    Handle mixed long-steel inventories where rebar, round bar, sections and fabricated bundles require controlled segregation.

    Truck and Rail Loading

    Load or unload bundles while respecting vehicle geometry, exclusion zones, trailer support points and secured-load procedures.

    Outdoor Rebar Yard

    Serve covered or open storage with project-specific wind, rain, corrosion, temperature and electrification provisions.

    Components and Operating Principle

    1. Bridge and end carriages: carry the trolley and distribute vertical, longitudinal and transverse reactions to the runway.
    2. Hoisting and trolley mechanisms: provide main and creep speeds selected from cycle time, placement tolerance and load control.
    3. Lifting beam: establishes the pickup-point spacing needed to control long bundles and may be fixed, rotating or telescopic.
    4. Load-engagement system: uses purpose-selected magnets, sling points, protected hooks, clamps or a combination arrangement.
    5. Power and controls: coordinate crane motions, magnet circuits, attachment status, limits, alarms and optional WMS/MES communication.
    6. Safety and feedback: monitor overload, position, travel limits, skew or anti-collision functions, magnet state and permitted release conditions.
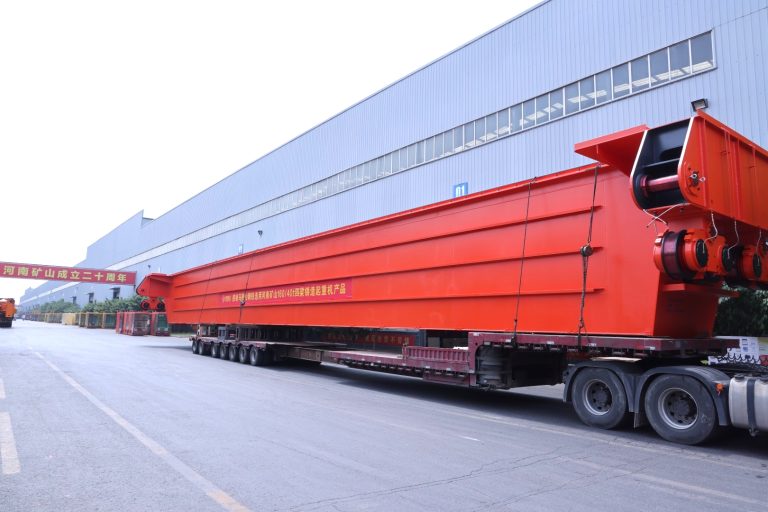
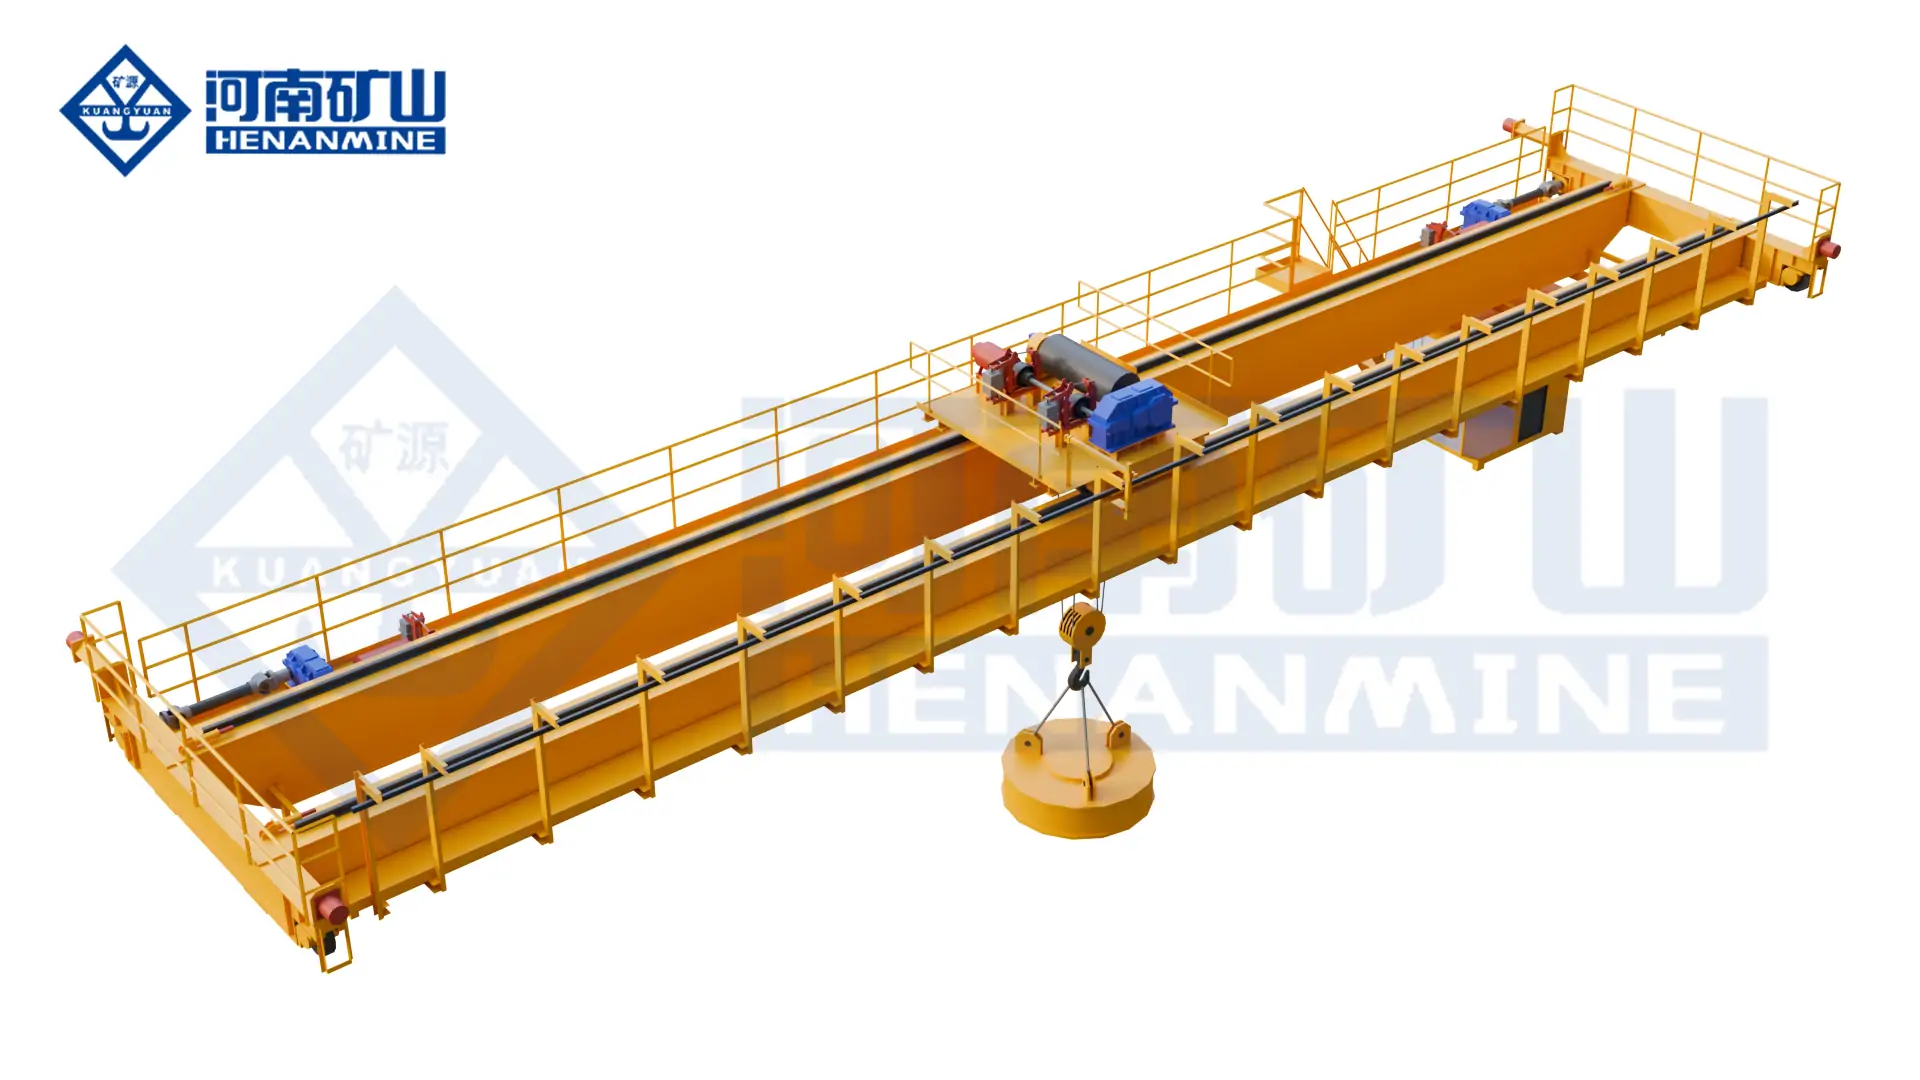
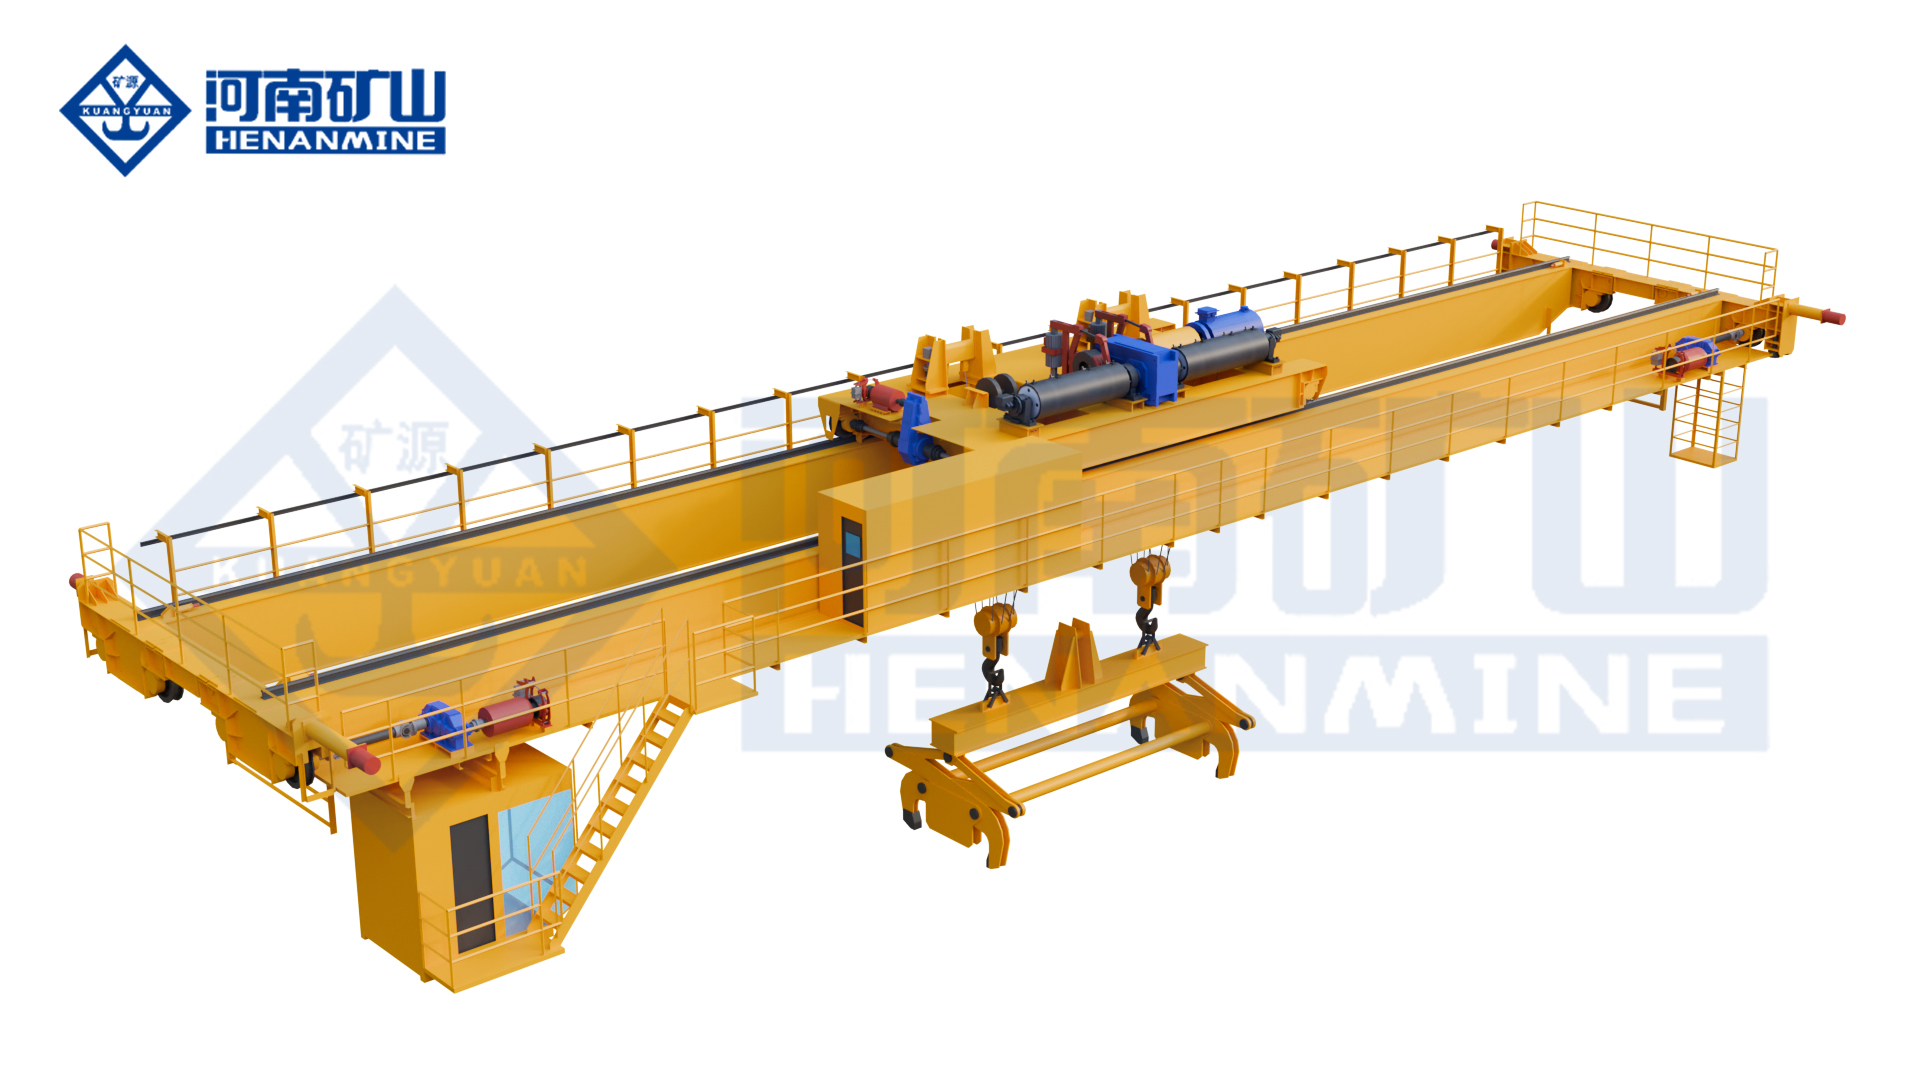
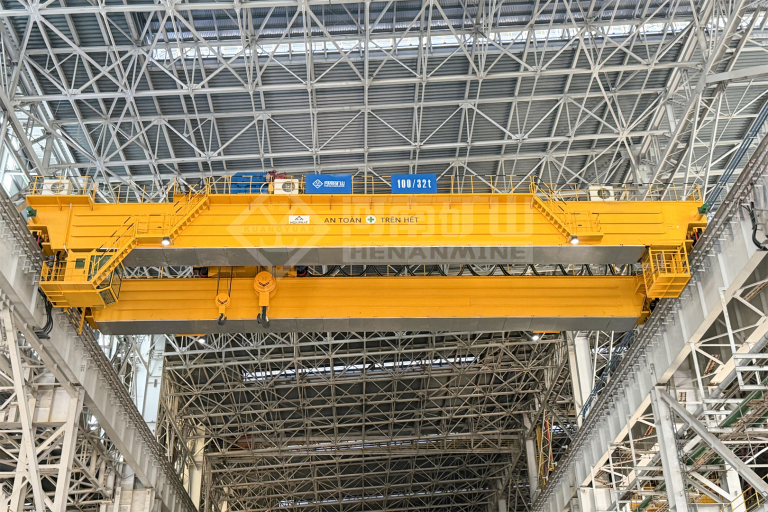
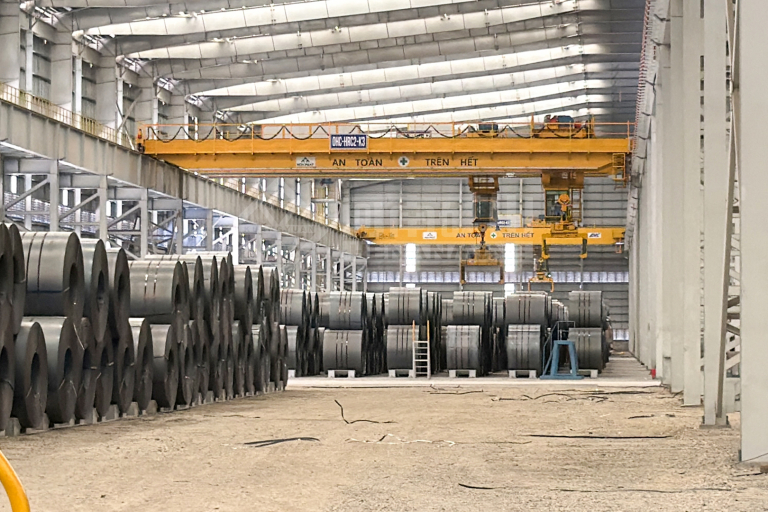
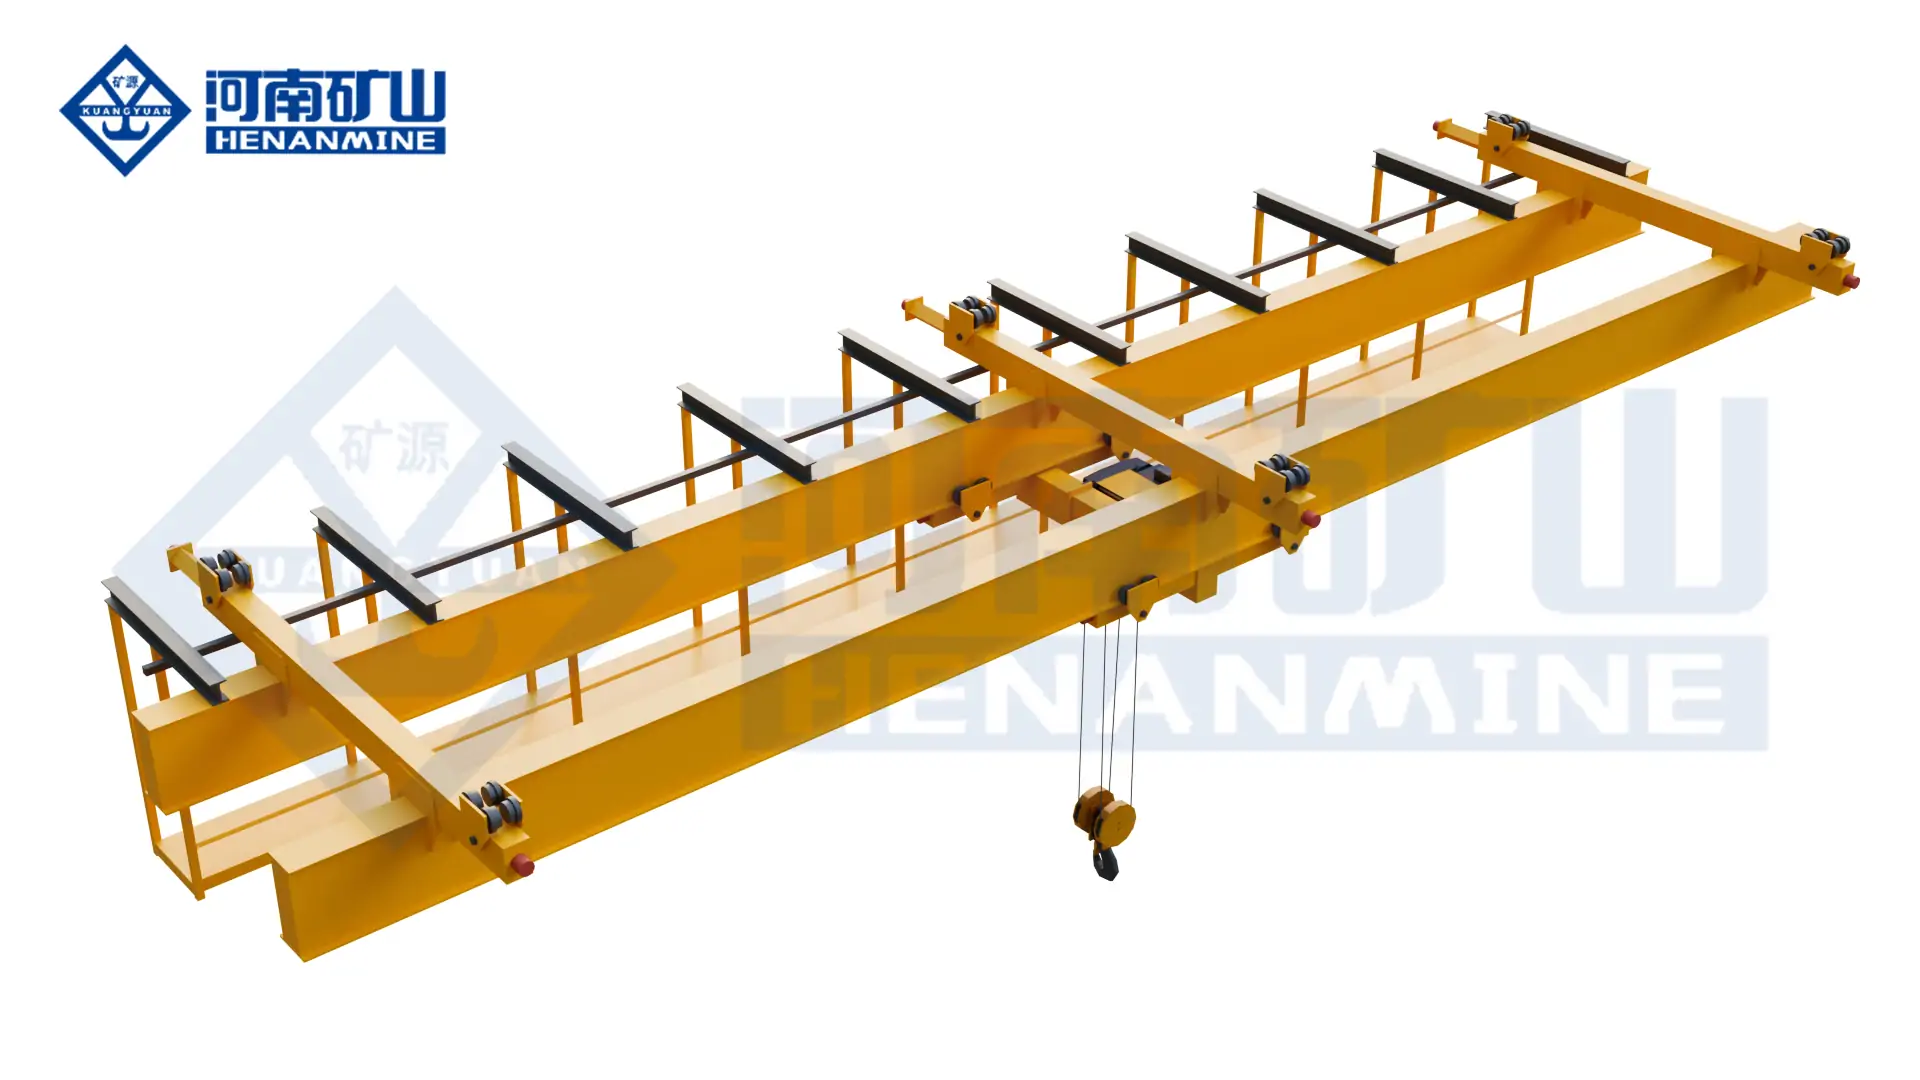
    rotating electromagnetic beam crane arrangement for long steel material transfer
    Beam length, magnet spacing, rotation envelope and end approach are coordinated with every pickup, rack and dispatch position.

    Capacity basis: the crane is sized for the maximum gross suspended load, including rebar, lifting beam, magnets or clamps, hook block, cables and every other below-hook component. A bundle payload cannot be used as the crane rating without adding the attachment mass and design effects.

    Rebar Handling Crane Selection Considerations

    Selection begins with the complete rebar and route matrix rather than a nominal tonnage. The following inputs determine the crane, beam, pickup method and controls.

    Bundle Matrix

    Minimum and maximum mass, bar length and diameter, bundle diameter or width, bars per bundle, number of bundles per lift and center-of-gravity variation.

    Material and Surface

    Steel grade and magnetic response; black, galvanized, epoxy-coated or stainless surface; temperature, scale, oil, moisture and acceptable contact marks.

    Bundle Integrity

    Tie type, quantity and position; loose or nested bars; permitted sag; overhang; separation method; damaged-bundle and partial-bundle handling procedure.

    Duty and Throughput

    Lifts per hour, shifts, annual hours, load spectrum, travel distances, required cycle time, peak dispatch rate and production consequence of downtime.

    Storage and Vehicle Interface

    Rack or dunnage geometry, stack height, aisle width, truck or rail-car profile, pickup clearance, release height, exclusion zones and required rotation.

    Building and Integration

    Rail-center span, runway length and elevation, wheel-load limits, headroom, approaches, power supply, cabin visibility, positioning tolerance and WMS/MES protocol.
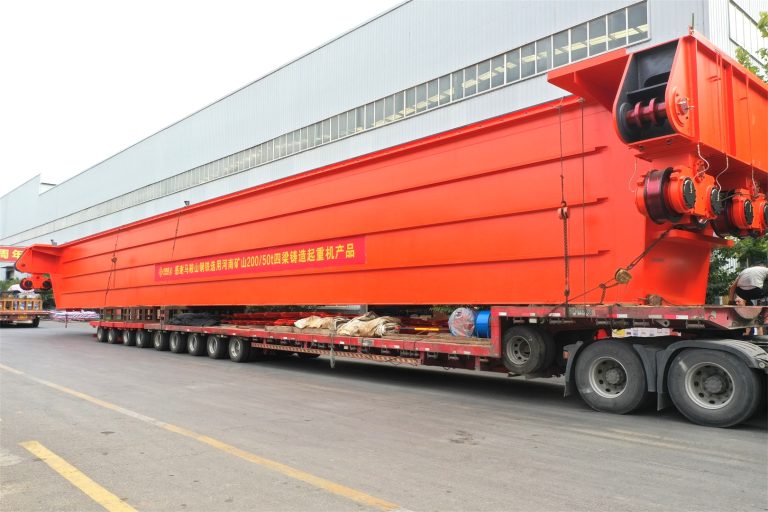
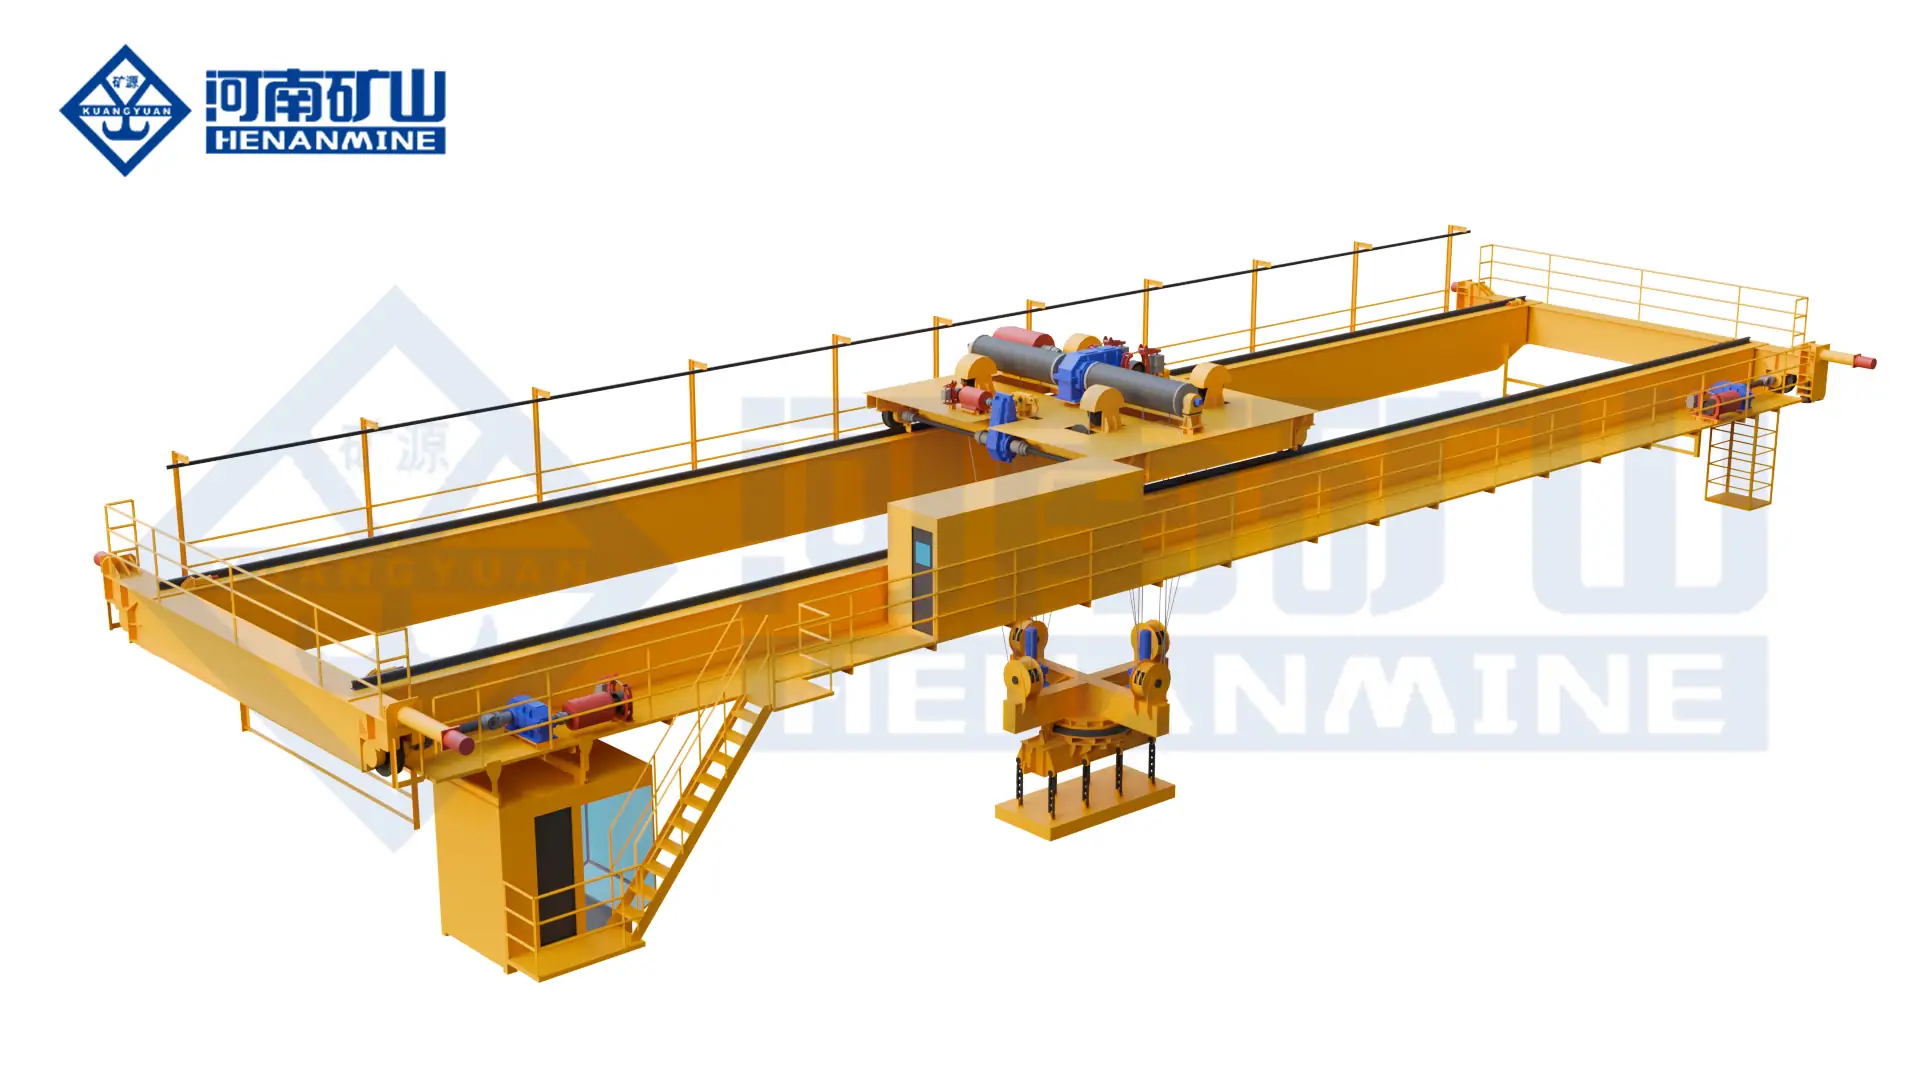
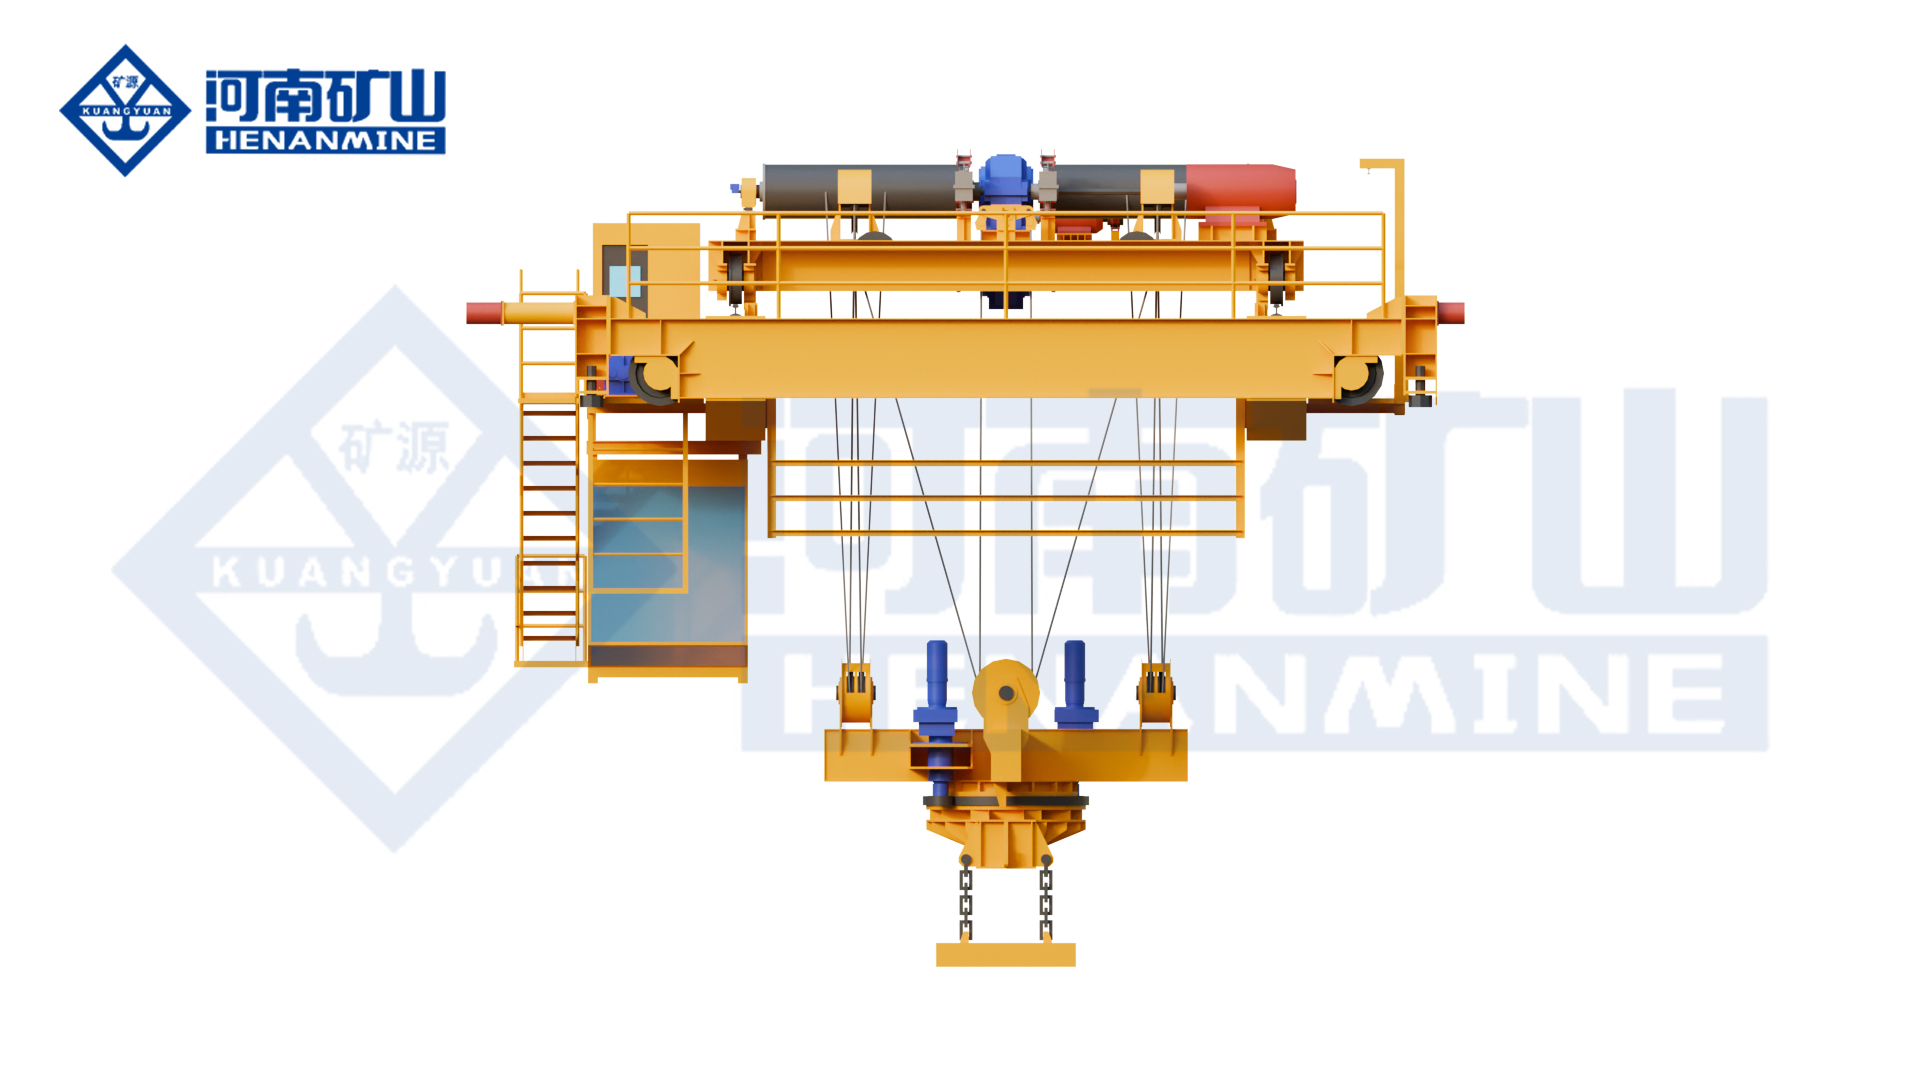
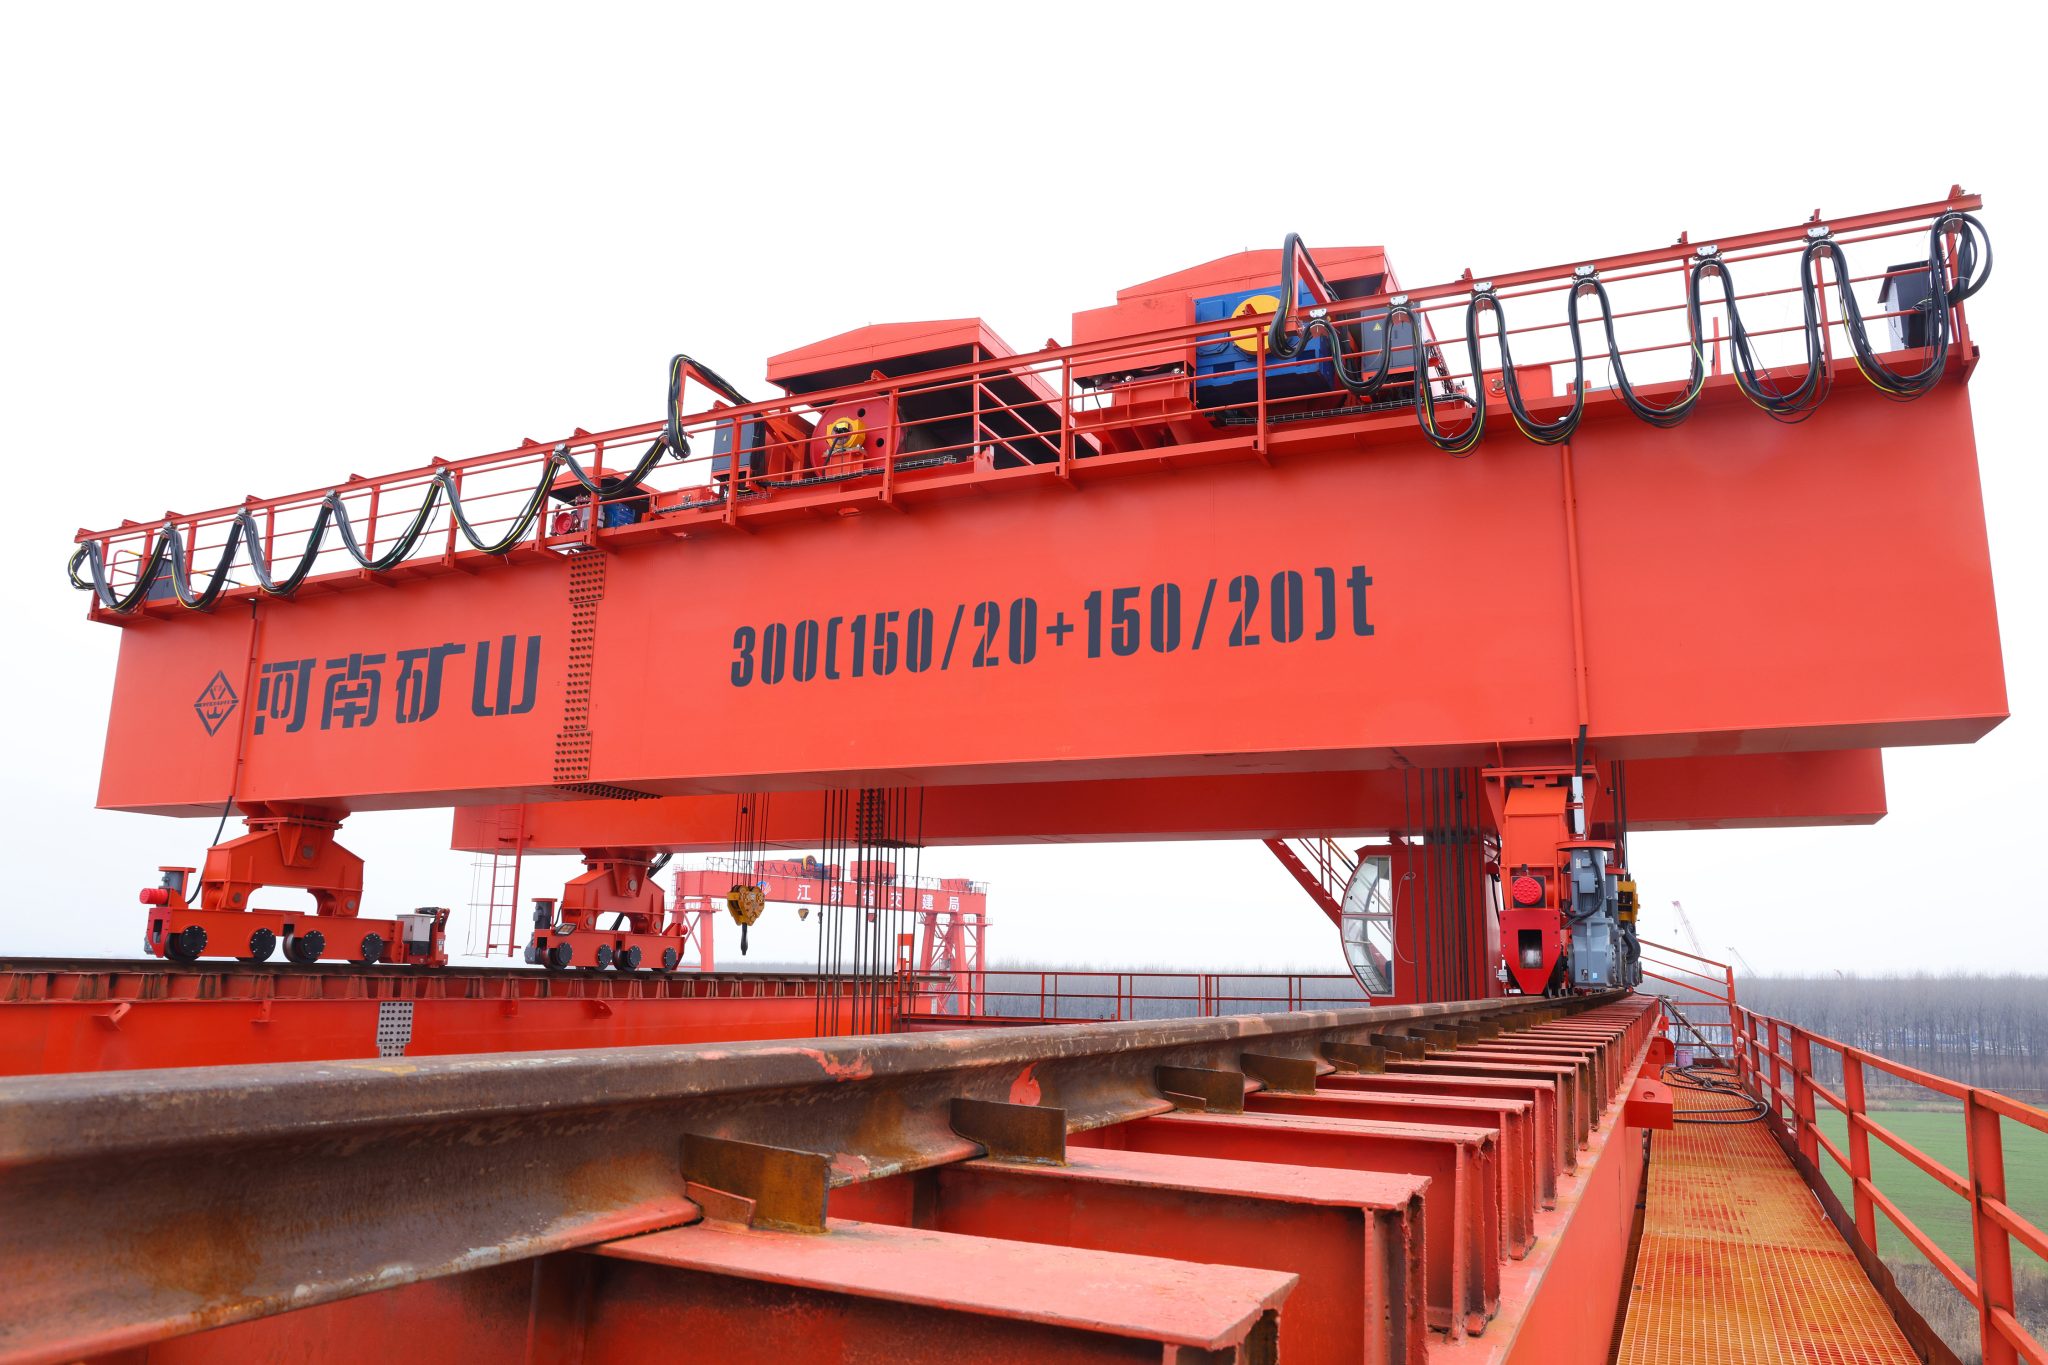
    electromagnetic beam crane engineering platform for rebar bundle handling selection
    The complete operating envelope includes beam rotation, magnet or sling approach, bundle overhang, adjacent stacks, building columns and vehicle clearances.

    Rebar Handling Crane Configurations Compared

    The lifting method is selected from the rebar grade, coating, bundle condition, throughput and layout. No single configuration is appropriate for every reinforcing-steel product.

    Configuration Suitable Handling Pattern Engineering Advantages Critical Limitations and Controls
    Fixed Electromagnetic Beam Crane Repeated transfer of validated ferromagnetic black-rebar bundles in one principal orientation Fast pickup and release without manual sling connection; multiple magnets distribute support Magnetic test, bundle retention, air gaps, temperature, power-failure strategy and fixed orientation
    Rotating Electromagnetic Beam Crane Warehouses or loading bays requiring bundle alignment at different angles Combines magnetic pickup with controlled horizontal orientation and compact stacking Higher headroom, rotation envelope, slewing lock, cable management, controls and maintenance scope
    Hook Crane with Spreader Beam and Slings Mixed grades, coated bars, low-to-medium cycles and nonmagnetic or uncertain materials Broad material compatibility and visible mechanical support at defined pickup points Manual rigging exposure, sling-angle effects, coating protection, tag-line rules and longer cycle time
    Mechanical Rebar Clamp or Tong Crane Standardized bundle sizes requiring powered engagement without magnetic pickup Positive mechanical engagement and possible automation for a controlled bundle envelope Contact pressure, bundle-size range, open/closed feedback, retention and protected contact faces
    Automatic Rebar Warehouse Crane High-volume storage with stable product data, fixed coordinates and controlled traffic zones Automated task execution, inventory traceability, sequencing and repeatable placement Reliable identification, position feedback, zone control, WMS/MES interface and recovery logic

    A rotating magnetic beam can reduce manual intervention and improve storage density, but it adds slewing machinery, magnet circuits, sensors, emergency-power provisions and software. Lifecycle maintenance and production-critical spares should be evaluated together with the initial equipment price.

    Rebar Handling Crane Technical Specification Framework

    Final values are confirmed on the approved technical schedule. Published product-family positions support preliminary configuration but do not establish a guaranteed rebar-handling combination.

    Specification Item Required Input Engineering Output Contract Evidence
    Rated load Maximum rebar plus complete beam, magnets, rigging and block Crane rating and permitted attachment combinations Load schedule and nameplate basis
    Bundle envelope Length, mass, diameter, bar count, grade, coating and bundles per lift Approved handling matrix and pickup-point arrangement Attachment data sheet and operating limits
    Span, lift and approaches Runway drawings, rail centers, elevations, rack and vehicle clearances General arrangement and complete load coverage Approved GA and clearance study
    Duty classification Load spectrum, lifts, starts, shifts, annual hours and process criticality Crane and mechanism classifications under the chosen standard Duty calculation and design basis
    Motion performance Cycle target, travel distances, placement tolerance and permitted sway Main/creep speeds, acceleration, braking and anti-sway functions Drive schedule and witnessed cycle test
    Runway reactions Building capacity, rail, supports and permissible horizontal loads Maximum/minimum wheel loads and longitudinal/transverse forces Reaction schedule for structural approval
    Controls and interfaces Operating modes, location accuracy, identification, zones and WMS/MES messages Control narrative, I/O, protocols and fallback mode Functional specification and acceptance test

    Published Henan Mine Crane Reference Platforms

    Product Platform Published Position Possible Rebar Role Application Boundary
    Upper-Rotating Magnetic Overhead Crane 5+5 t to 25+25 t; 10.5–31.5 m span; 6–20 m lift; A6–A7 Long bars requiring rotation, alignment and grouped magnetic pickup Published notation must be reconciled with total payload, beam and magnet mass
    Electromagnetic Bridge Crane 5–32 t including electromagnet; 10.5–31.5 m span; 6–30 m lift Ferromagnetic steel transfer using a project-selected magnet system Bar geometry, bundle retention, duty and magnetic performance require validation
    Electromagnetic Hanging Crane 5–50 t; 10.5–31.5 m span; 6–20 m lift; A6–A7 Fixed or rotating-beam long-steel handling Final magnet array, temperature range and retention strategy are process-defined
    Custom Spreader, Sling or Clamp Crane Project-defined capacity, beam length, span, lift, duty and speeds Coated, nonmagnetic, mixed or irregular reinforcing-steel products Final configuration follows representative-load trials and the approved handling matrix

    Published ranges describe product families. They are not a promise that every capacity, span, lift, duty and attachment can be combined in one crane.

    Rebar Bundle and Lifting-Attachment Engineering

    Long bundles need several support or pickup points. Magnet quantity and spacing, sling separation or clamp location are established from the maximum length, minimum bundle stiffness, permissible sag and center-of-gravity range. The outer pickup points must control end droop without overstressing individual bars or bundle ties.

    Representative-load trials are required when lifting performance depends on magnetic contact, friction, coating, bar nesting, tie condition or automated bundle recognition. A solid test weight does not reproduce the air gaps and bar-to-bar movement of a real rebar bundle.
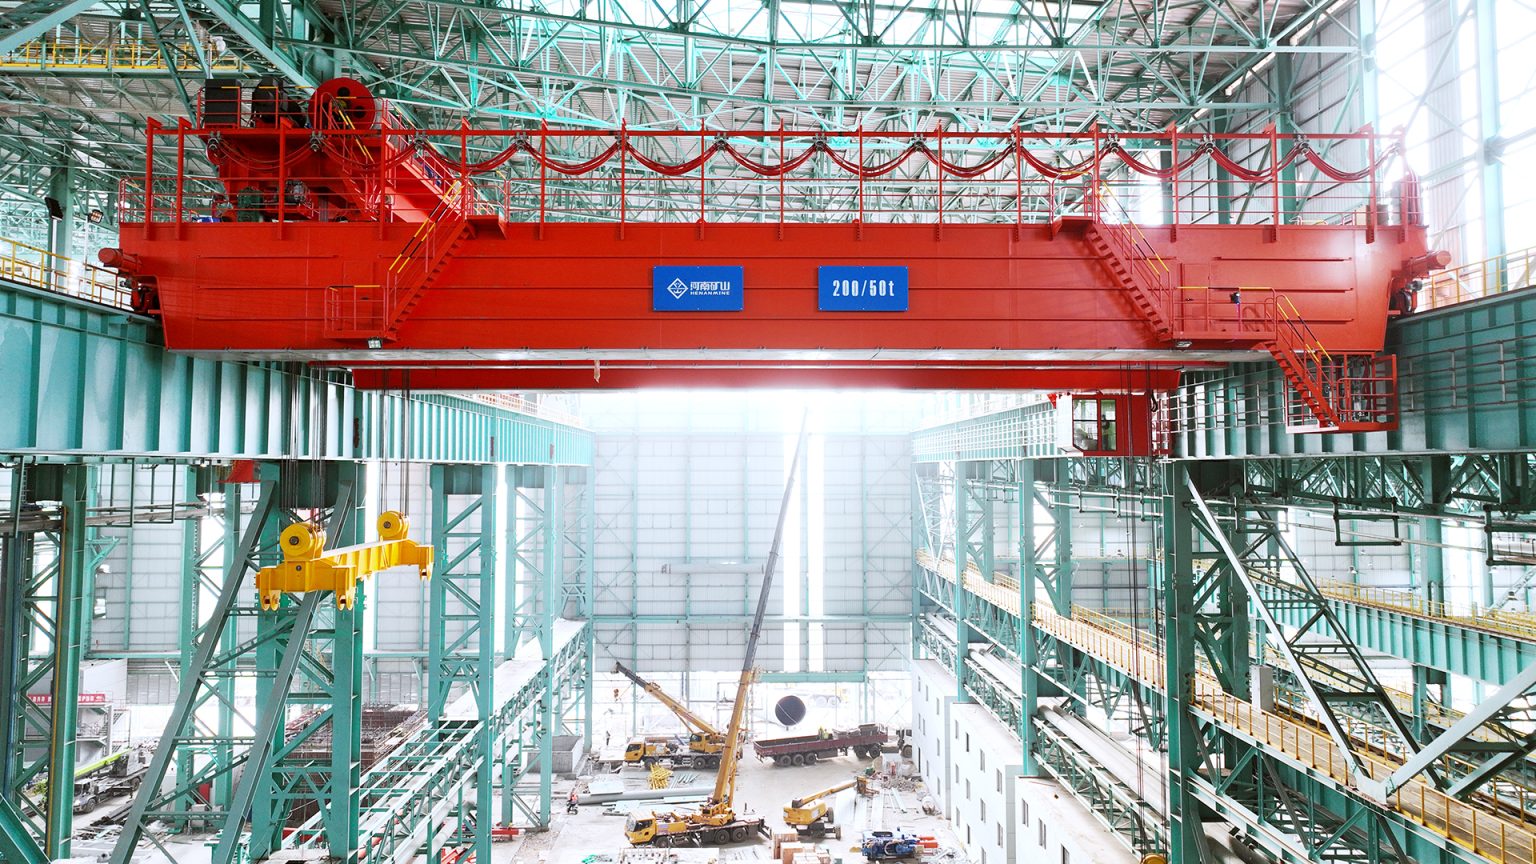
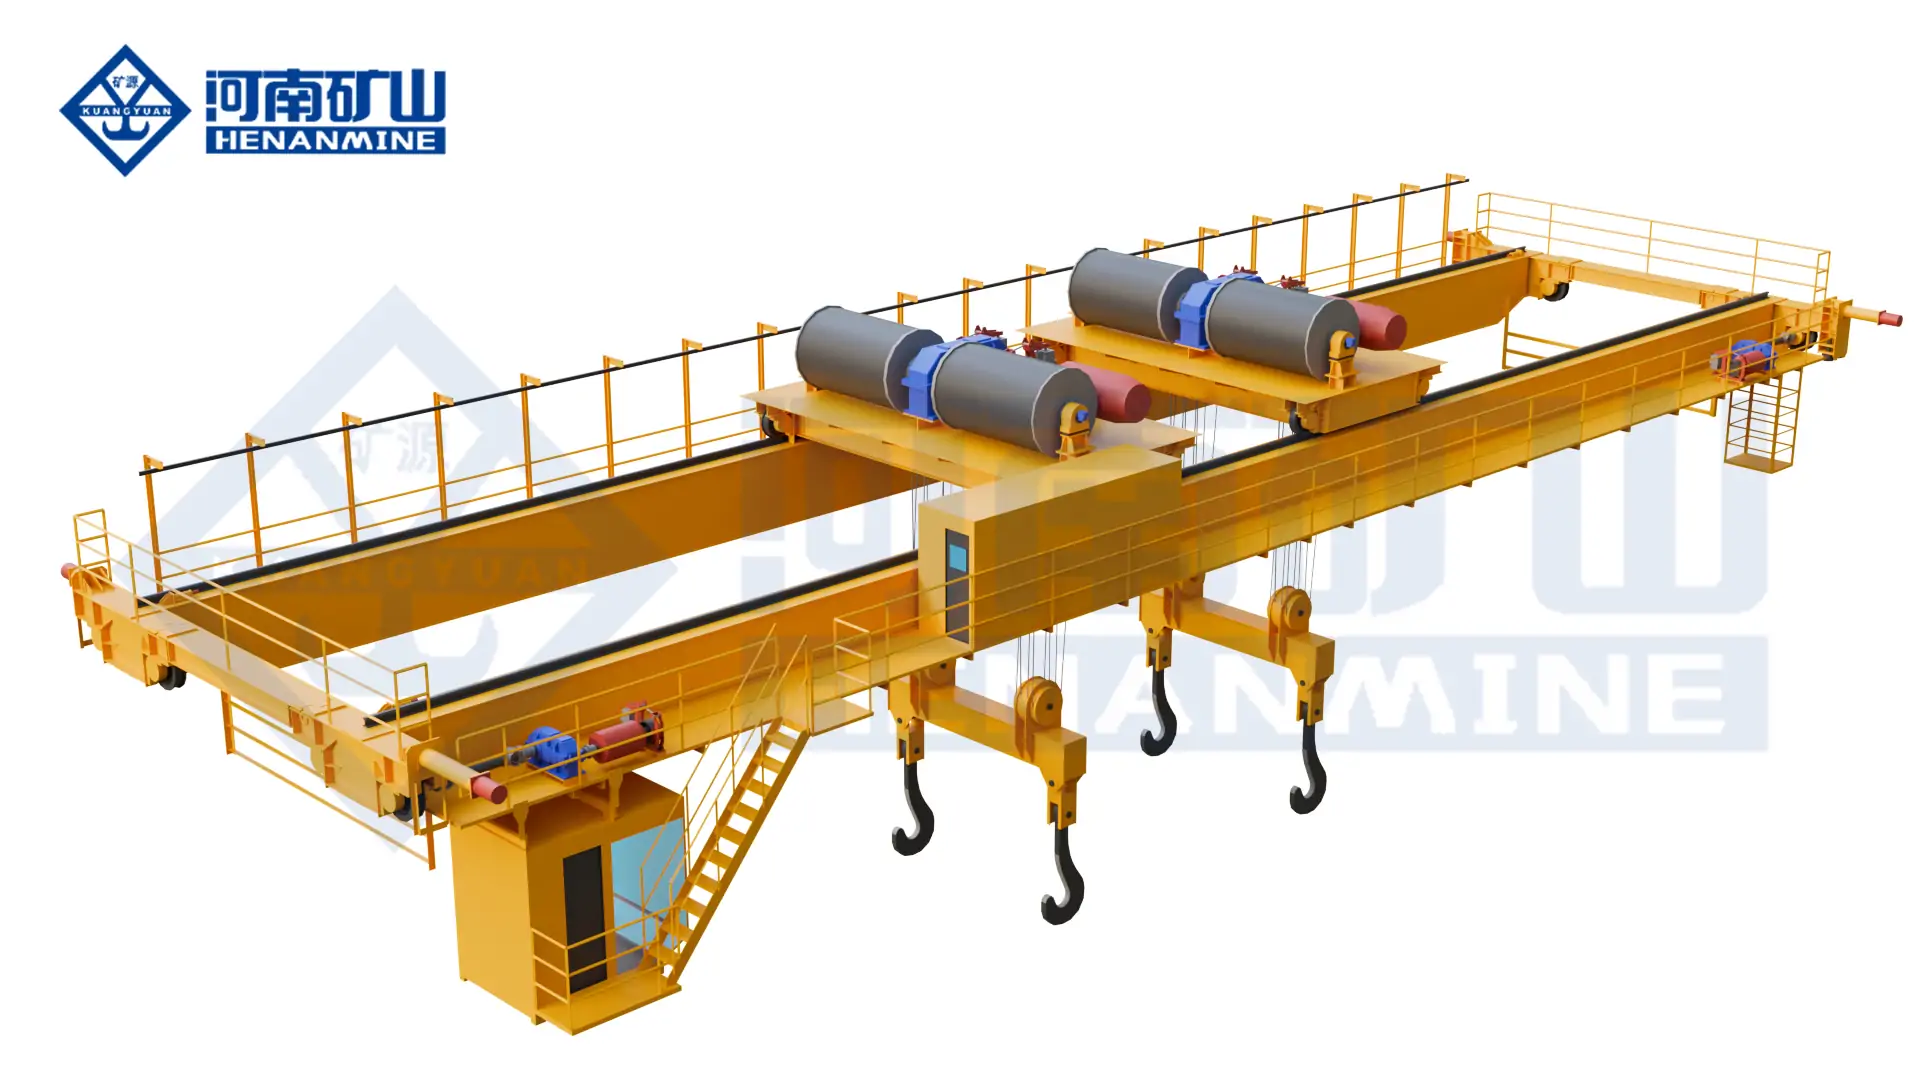
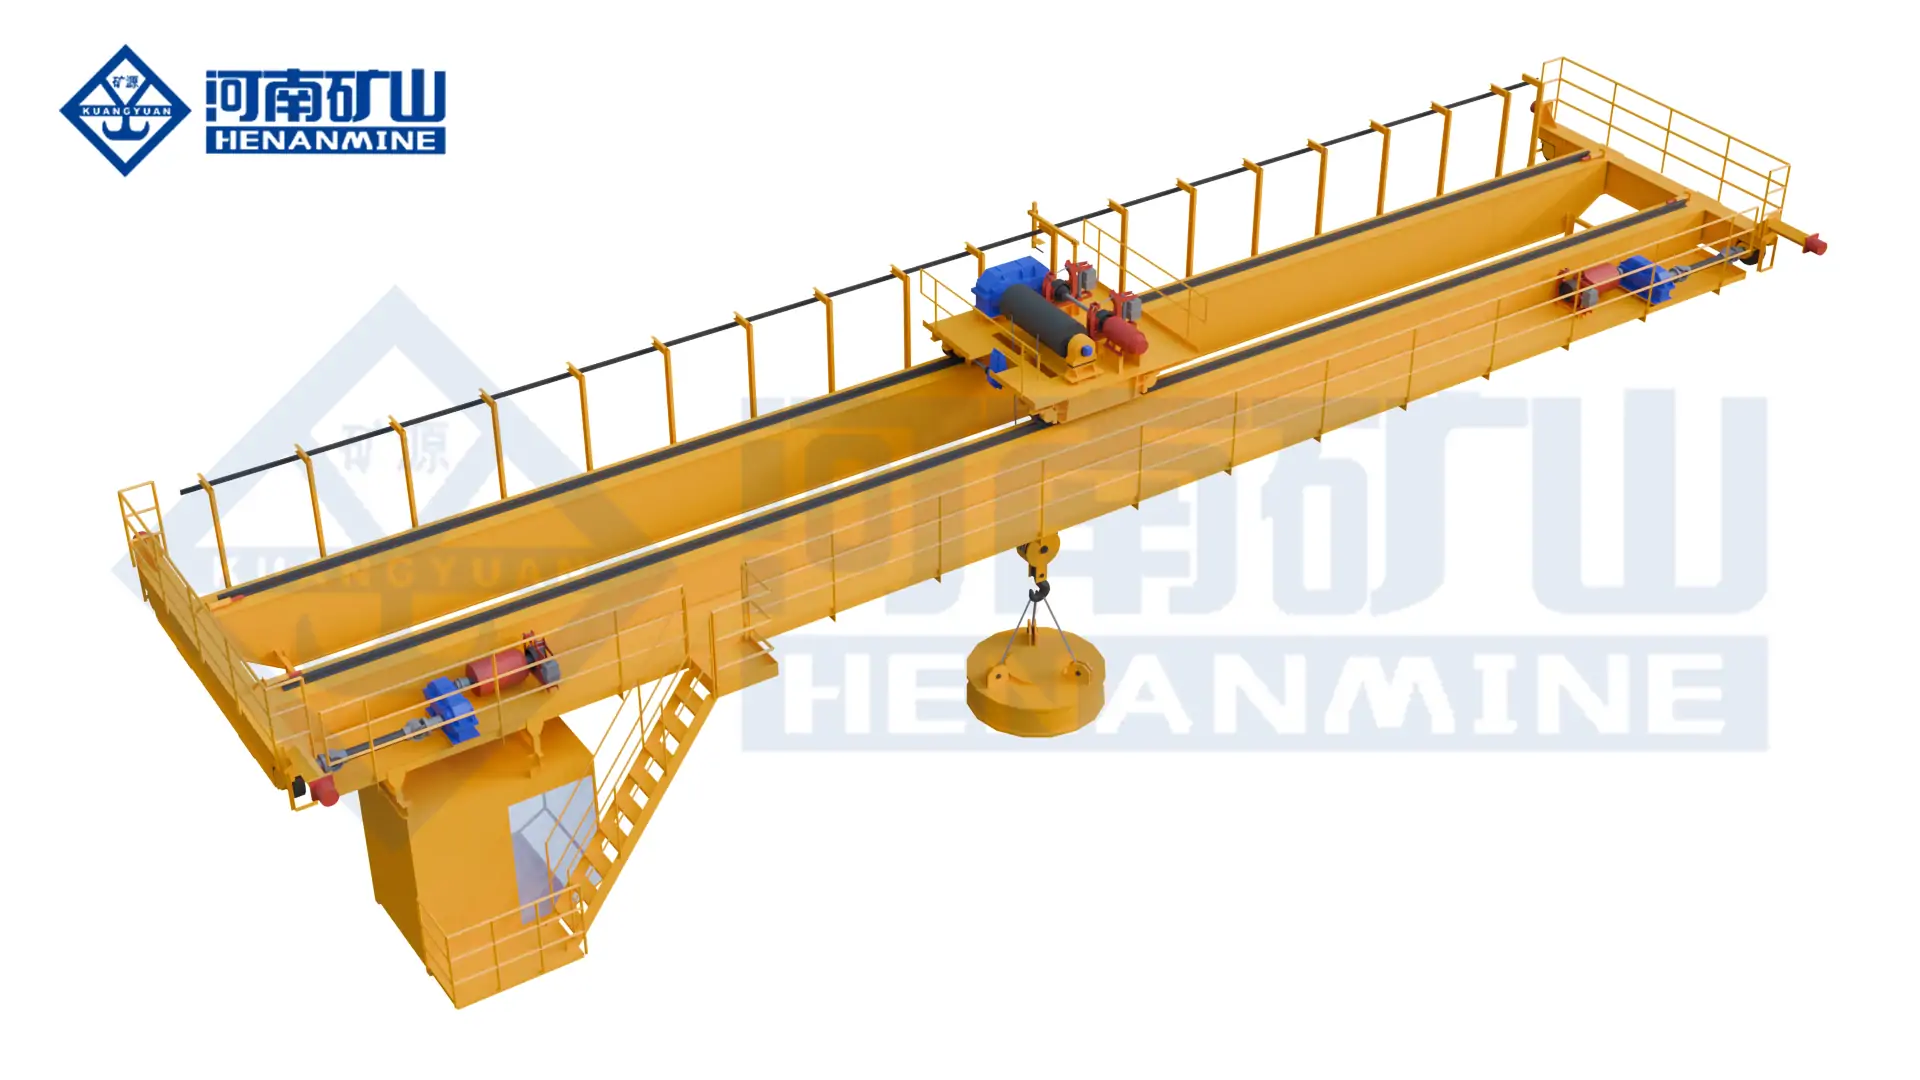
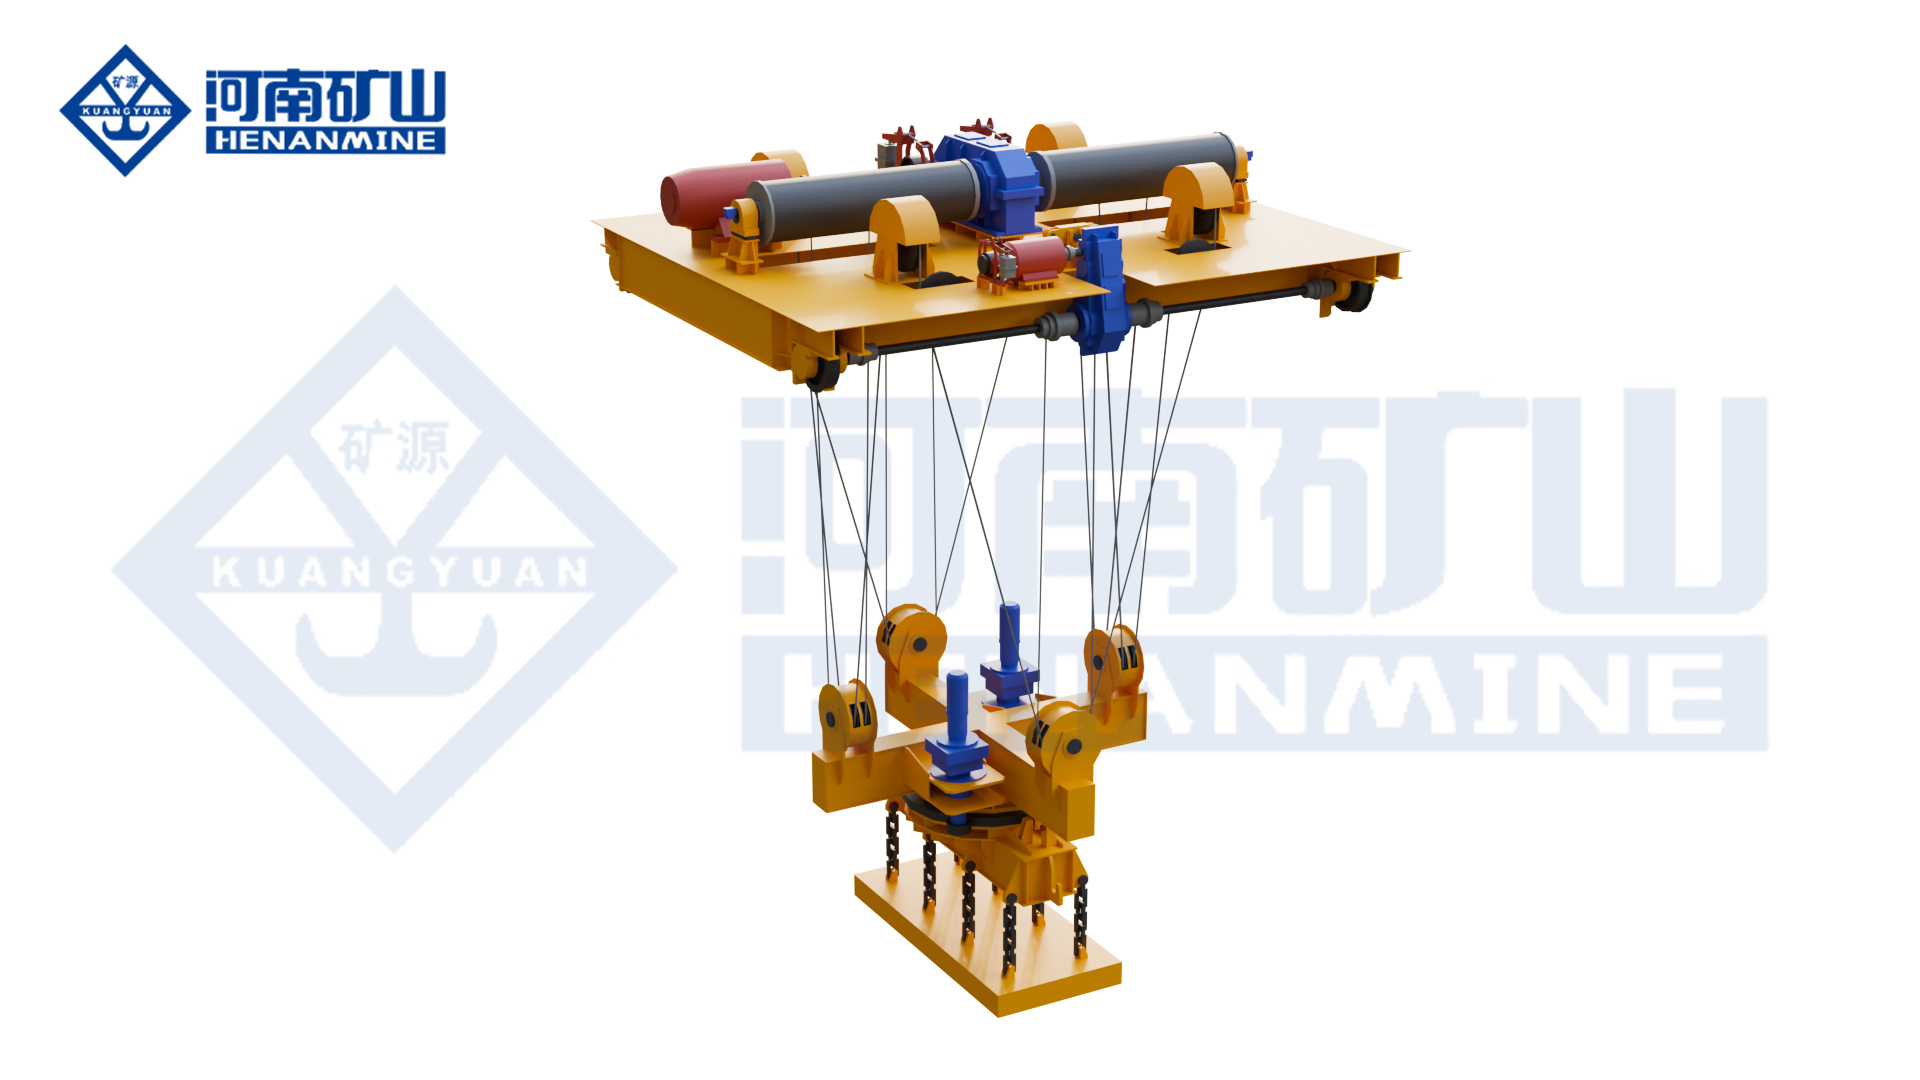
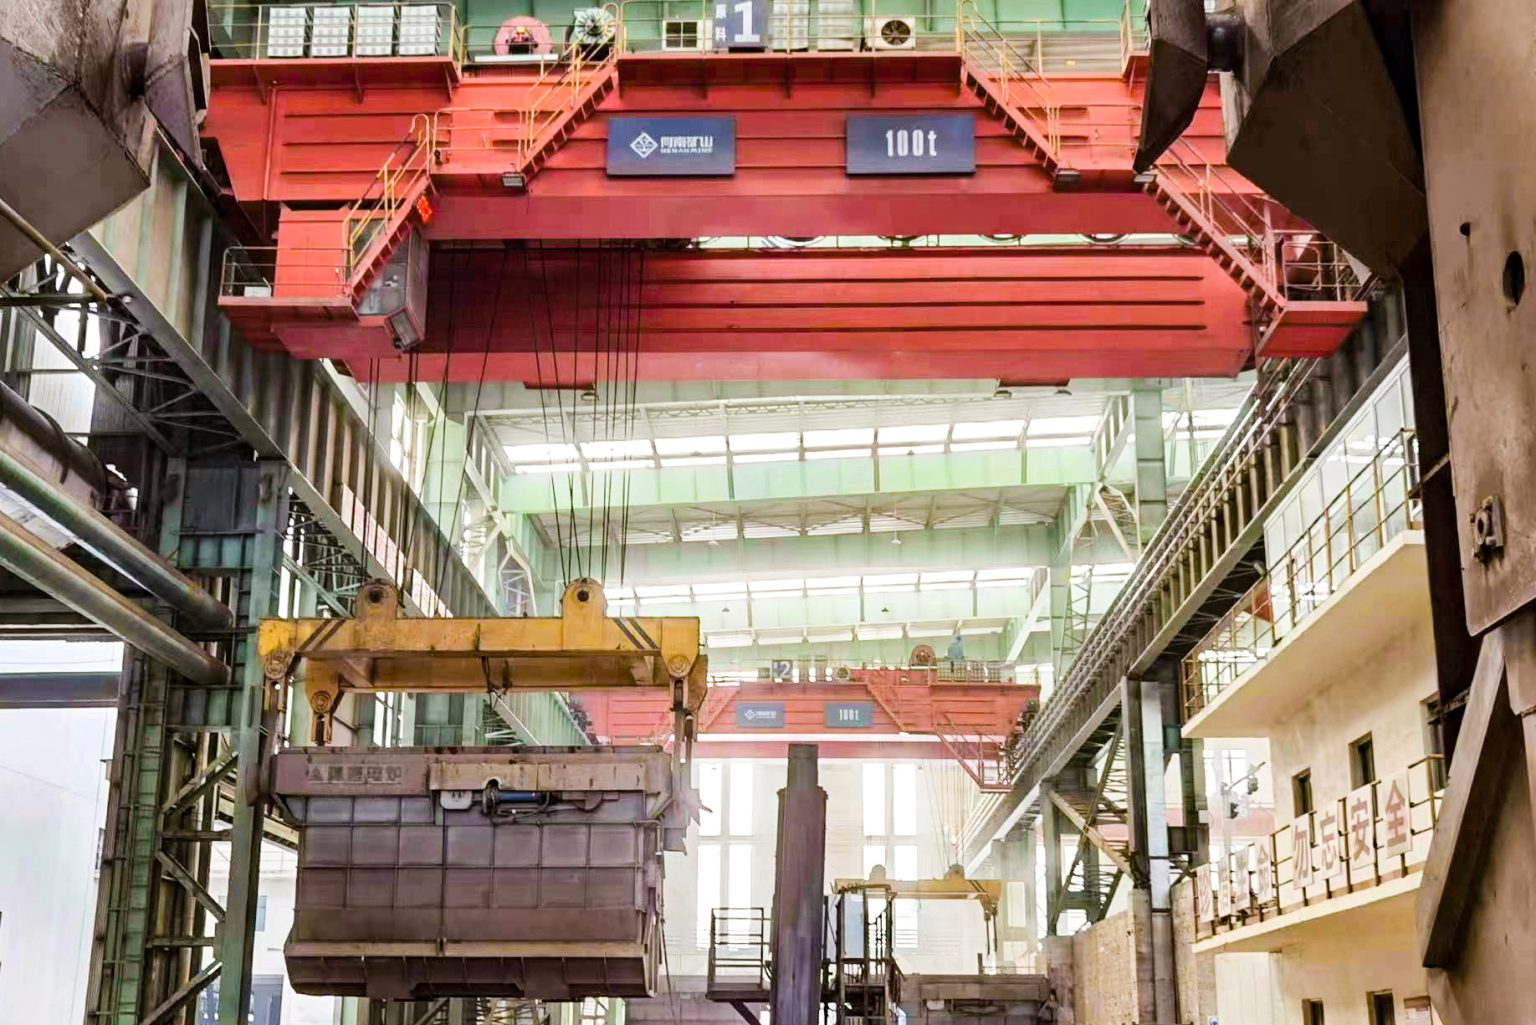
    engineered rotating beam and magnet arrangement for long rebar bundles
    The final magnet or lifting-point array is verified against the shortest, longest, lightest, heaviest and least favorable bundle conditions.

    Magnet Array

    Magnet type, pole geometry, grouped excitation, current control and spacing follow bar diameter, bundle profile, air gaps, temperature and required pickup combinations.

    Spreader and Sling Geometry

    Beam length, sling angles, rated components, protective sleeves and pickup spacing prevent excessive bending and coating damage.

    Rotation and Telescoping

    Rotation is justified by the rack and vehicle approach; telescoping is justified by a wide length range. Both functions require mechanical limits, interlocks and maintenance access.

    Illustrative Long-Rebar Duty

    For an illustrative duty involving three bundles at 3.5 t each and 9–12 m long, the payload is 10.5 t before adding the beam, magnets, cables and block. Crane capacity, magnet grouping, beam deflection, emergency retention and runway reactions must therefore be calculated from the gross suspended mass—not from a single 3.5 t bundle. This example explains the sizing method and is not a standard rating or delivered-project claim.

    Handling Black, Galvanized, Epoxy-Coated and Stainless Rebar

    Rebar Condition Primary Handling Concern Typical Engineering Direction Required Verification
    Black carbon-steel rebar Irregular rib contact, scale, rust, air gaps and bundle movement Validated magnetic beam or multi-point mechanical lift Worst-case representative bundle and secure retention of all bars
    Galvanized rebar Zinc surface marking, abrasion and contamination Protected slings or qualified contact system; magnet only after testing and surface approval Permitted marks, contact material and customer coating requirements
    Epoxy-coated rebar Chipping, scratching, local pressure and impact damage Padded spreader, synthetic slings or approved protected clamp; avoid unprotected chains and dragging Applicable coating specification, allowable damage and repair procedure
    Stainless or specialty rebar Magnetic response varies by alloy and processing condition; ferrous contamination may be prohibited Dedicated protected mechanical system unless magnetic suitability is formally proven Alloy, magnetic test, contamination controls and segregated rigging requirements

    Load Stability, Magnetic Safety and Release Control

    Magnet-Proven Load Envelope

    Every approved grade, diameter, bundle shape, temperature and pickup combination is documented.

    Power-Failure Retention

    Emergency supply or electro-permanent strategy, monitoring and safe-lowering time are defined by risk assessment.

    Release Interlock

    Demagnetization or clamp opening is permitted only inside the defined placement zone and release-height window.

    Traffic and Collision Control

    Crane separation, restricted zones, vehicle presence and end approaches are supervised by agreed devices and logic.

    Motion Control

    VFD acceleration, braking, creep speed and optional anti-sway reduce bundle movement near racks and vehicles.

    Inspection Access

    Walkways and service positions support inspection of ropes, brakes, beam structure, magnets, cables and attachment pins.
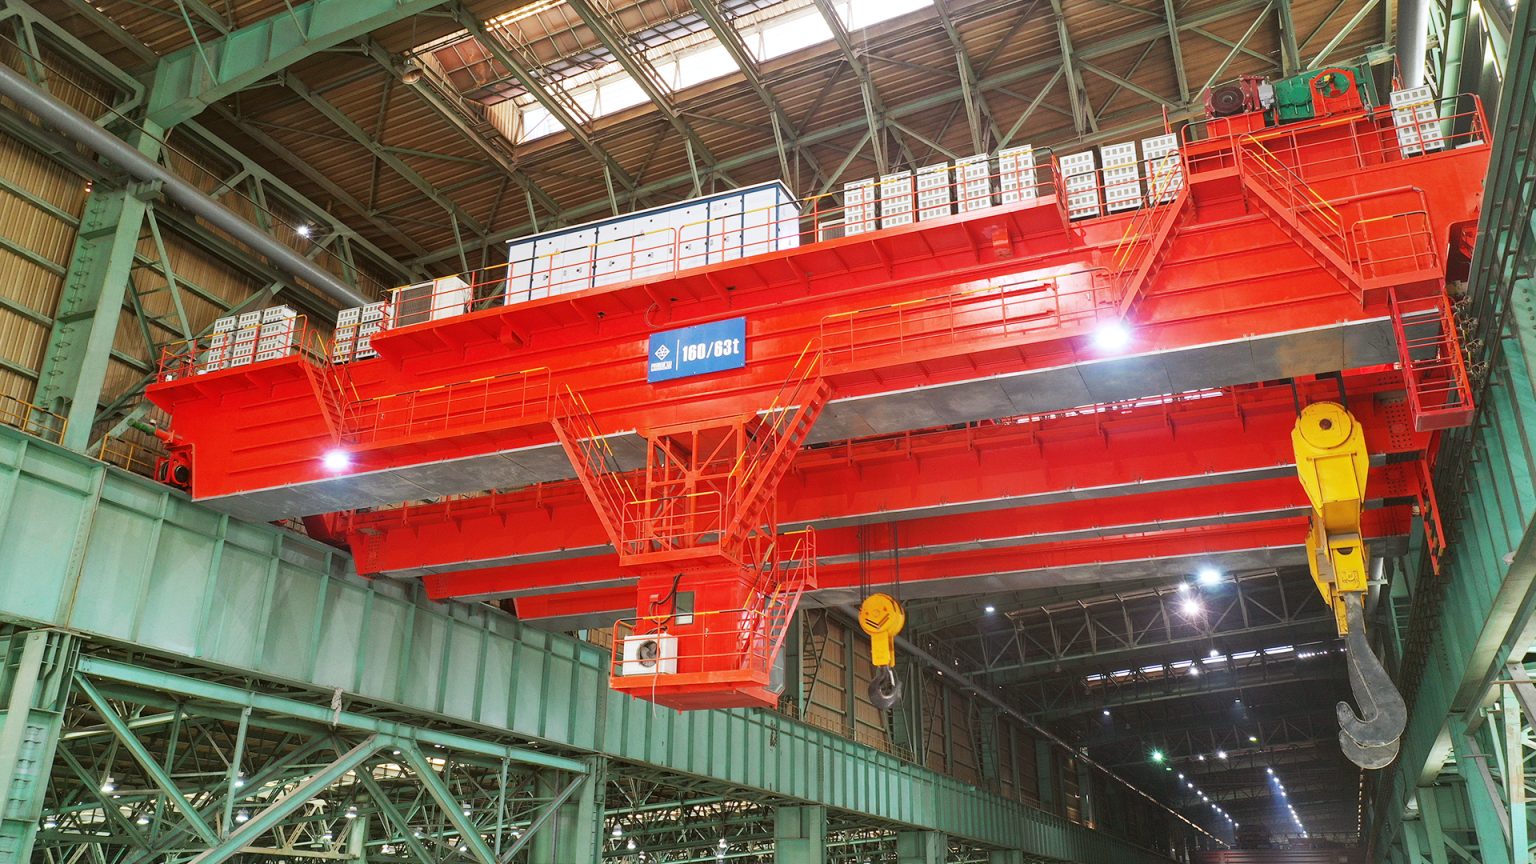
    electromagnetic beam overhead crane safety and retention system
    Magnetic status, emergency retention, rotation lock and release permission form one coordinated safety function.

    Manual, Semi-Automatic and Automatic Rebar Handling

    Automation level follows product repeatability, inventory data quality, traffic risk, throughput and the facility’s ability to maintain sensors, networks and software.

    Control Level Typical Functions Appropriate Conditions Required Definition
    Manual control Cabin or radio control, variable speeds, load display, cameras, magnet controls and interlocks Mixed products, irregular bundles and experienced operator supervision Sightlines, operator location, communication, rigging access and exclusion zones
    Semi-automatic Automatic travel or rotation to stored positions with operator-authorized pickup and release Repeated racks or loading stations with occasional exceptions Target coordinates, handover points, confirmation logic and exception recovery
    Fully automatic Task receipt, bundle identification, pickup, transport, stacking, retrieval and completion feedback Controlled warehouses with standardized bundles, stable data and segregated traffic WMS/MES interface, coordinate system, safe-state logic, cybersecurity and manual fallback

    Bundle Identification

    Barcode, RFID, production data or machine vision associates each bundle with heat, grade, diameter, length, mass, order and storage position.

    Positioning and Anti-Sway

    Absolute position feedback, rotation sensing and load-dependent motion control support repeatable pickup and placement.

    Inventory Integration

    The interface defines task ownership, material identity, source, destination, status, alarms, time synchronization and recovery after communication loss.
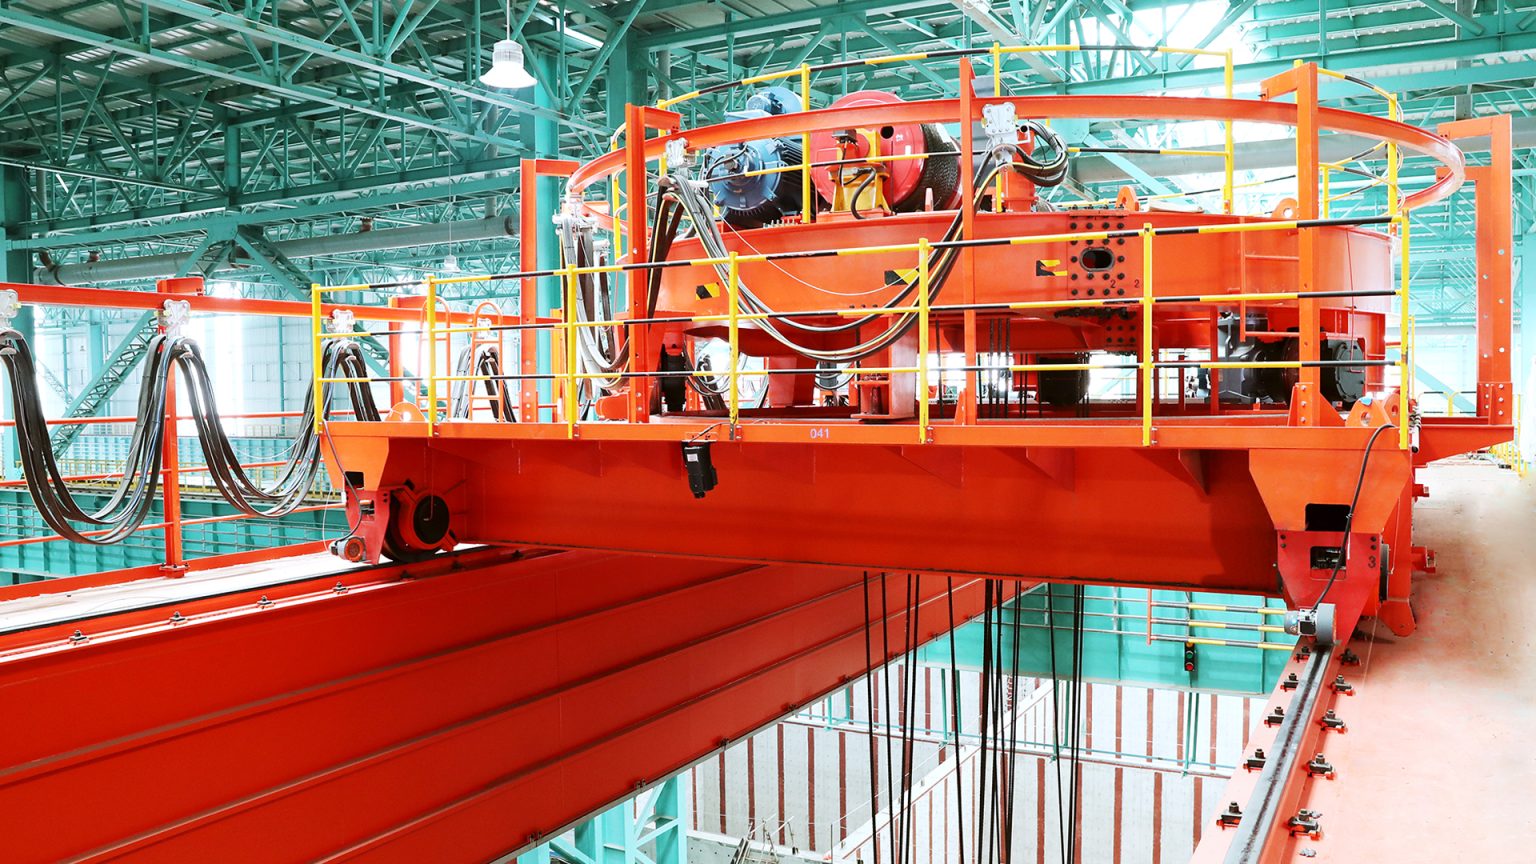
    automated rotating electromagnetic beam crane for steel warehouse material flow
    Automatic operation requires controlled storage coordinates, dependable bundle data, protected traffic zones and a defined manual-recovery procedure.

    Design Basis, Inspection and Acceptance

    The purchase specification identifies one coherent design route. Local statutory requirements remain applicable at the installation site, and standards from different systems are not combined selectively without an approved compliance matrix.

    Possible Design Routes

    A project may use ISO crane-classification principles with applicable crane and electrical standards; EN 13001 with EN 15011 and EN 13155 where applicable; or a North American route using CMAA specifications with applicable ASME B30.2, B30.20 and ASME BTH-1 requirements. A Chinese-standard route may reference the applicable bridge-crane and lifting-magnet standards. The contract states the selected basis.

    Engineering Deliverables

    General arrangement, wheel loads, duty calculation, rebar matrix, beam and attachment data, magnetic study where applicable, clearance study, electrical drawings, control narrative, interface list, inspection plan and maintenance-access arrangement.

    Manufacturing Inspection

    Material traceability, welding procedures and welder qualification, specified NDT, dimensional checks, machinery alignment, beam and attachment inspection, electrical-panel inspection, cable management, coating and documentation records.

    FAT and Site Acceptance

    Functional tests verify motions, brakes, limits, overload protection, rotation, attachment engagement, alarms and available automation. Site tests then cover runway, erection, load testing, representative rebar bundles, power-loss response, placement tolerance, interfaces, training and handover.

    Relevant Long-Steel and Steel-Mill Experience

    Project references are evaluated by process similarity. The following Henan Mine Crane references demonstrate rotating electromagnetic material handling and process-based crane-fleet planning. A new rebar crane still requires its own bundle matrix, lifting study and acceptance criteria.
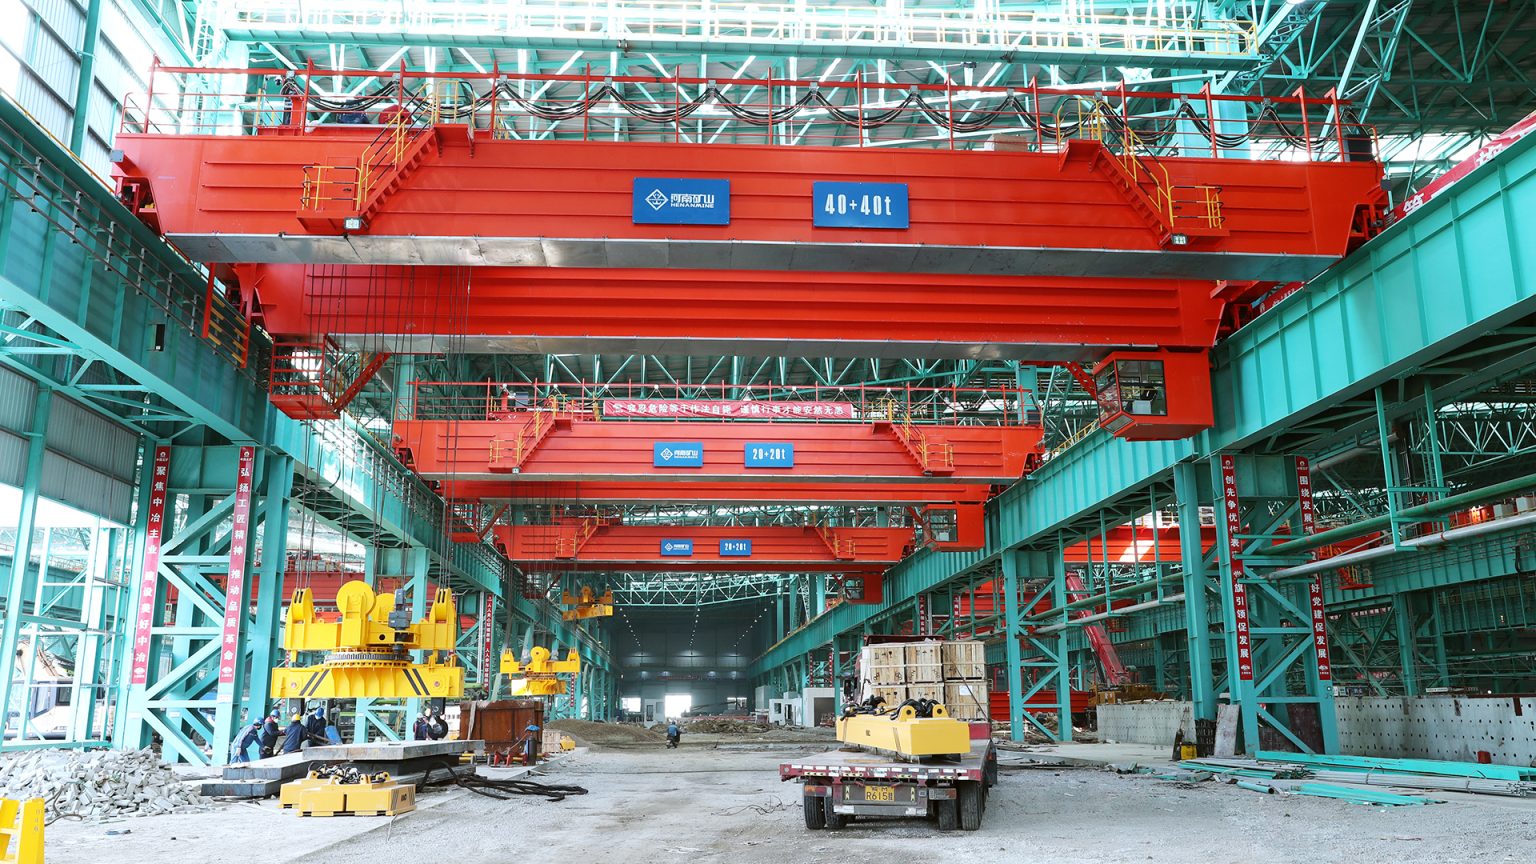
    Henan Mine Crane rotating electromagnetic beam crane steel handling reference

    Magnetic Long-Material Reference

    Overhead Rotating Electromagnetic Beam Crane

    The published platform combines a rotating trolley, electromagnetic beam, grouped magnetic control and variable-frequency motion for ferromagnetic steel-material transfer.

    These structural and control principles are relevant to straight-rebar warehouses, while the magnet geometry, bundle envelope and retention strategy remain rebar-specific.
    View Magnetic Crane Reference

    Henan Mine Crane hot rolling mill bridge crane fleet project

    Steel-Mill Fleet Reference

    34 Cranes for a 4.5-Million-Tonne Plate Facility

    Henan Mine Crane supplied 34 double-girder overhead cranes rated from 10 t to 100 t for production, roll handling, tooling, equipment service and maintenance.

    The reference demonstrates process-based fleet planning: rebar production, bundling, warehousing, dispatch and maintenance may require different capacities, speeds and attachments.

    View Steel-Mill Reference

    Reference boundary: these projects demonstrate relevant crane engineering, magnetic-material handling and steel-mill integration capability; they do not establish the final rating, magnet array, cycle performance or price of a new rebar handling crane.

    Rebar Handling Crane Price and Budget Scope

    A responsible rebar handling crane price requires the bundle matrix, lifting method, gross load, beam length, span, lift, duty, speeds, runway scope, controls and destination. Public prices are preliminary market signals rather than comparable project quotations.

    Public Market Signal Checked in September 2026 Published Position What It Indicates Commercial Limitation
    10 t rotating electromagnetic hanging-beam listing US$12,000 for 1–4 units; US$10,500 for 5+ units A low public equipment-listing entry point for a nominal magnetic-beam crane Does not normalize magnet array, true rebar duty, runway, freight, erection, testing or compliance
    10 t steel-bar handling crane listing US$26,000 for 25 m span, 12 m lift and A6 published duty A long-span, process-duty steel-bar crane carries a higher stated equipment value Attachment, controls, delivery boundary and acceptance tests are not fully normalized
    5+5 t steel-mill electromagnetic-beam project US$135,100 for 34 m span, 16 m lift and A6 published duty Large span, heavy-duty platform, cabin and project accessories can materially increase cost Published application is steel-pipe handling, not a like-for-like rebar quotation
    Automatic rebar warehouse crane Project quotation Budget includes crane, beam, identification, positioning, safety zones and software interfaces A complete functional specification, data interface and site boundary are required

    Major budget drivers: maximum gross suspended load; rebar length and bundles per lift; fixed, rotating or telescopic beam; magnet quantity and emergency supply; protected rigging or clamps; span, lift and approaches; working class; positioning and anti-sway; WMS/MES integration; cabin and environmental protection; runway and electrification; export packing, freight, erection, load tests and local compliance.

    The figures above are third-party public market observations, not Henan Mine Crane offers. Marketplace values may be placeholders, volume prices or equipment-only figures. Contract comparisons require a line-by-line technical and commercial scope reconciliation.

    Rebar Handling Crane RFQ Information

    A complete enquiry allows the crane, beam, pickup method, runway reactions, controls and commercial scope to be priced on the same basis.

    Rebar and Bundle Data

    Grade and magnetic properties; black, galvanized, epoxy-coated or stainless condition; minimum/maximum bundle mass, length and diameter; bar diameter; bars and bundles per lift; tie details; temperature; drawings and photographs.

    Process and Throughput

    Pickup and placement stations; storage sequence; lifts per hour; shifts; annual hours; load spectrum; travel distances; target cycle time; peak vehicle loading; production consequence of an outage.

    Building and Storage Layout

    Span, runway length, rail section and elevation; required lift; approaches; headroom; rack, dunnage, truck and rail-car drawings; existing wheel-load limits; installation access and site survey.

    Controls and Commercial Scope

    Manual or automatic operation; rotation; positioning tolerance; identification and WMS/MES protocol; voltage and frequency; environment; destination; design standard; Incoterm; runway, electrification, installation, testing and documentation scope.

    Frequently Asked Questions

    How is rebar handling crane capacity calculated?

    Capacity begins with the maximum total rebar payload and adds the lifting beam, magnets or clamps, rigging, hook block and all other suspended equipment. Duty, unbalanced loading and dynamic effects are then applied under the selected design standard.

    Can magnets safely lift rebar bundles?

    Only after validating steel grade, bar diameter, rib profile, bundle shape, air gaps, surface condition, temperature and retention of every bar. Representative bundles must be tested across the approved operating envelope.

    Is a fixed or rotating beam more suitable?

    A fixed beam is simpler where pickup and placement share one orientation. Rotation is justified where racks, lines or vehicles require different angles, but it adds headroom, machinery, controls and inspection requirements.

    How should epoxy-coated rebar be handled?

    The lifting system should use protected contact faces, padded spreaders or suitable synthetic slings under the applicable coating specification. Unprotected chains, sharp edges, dragging and uncontrolled impact should be excluded.

    How much does a rebar handling crane cost?

    Public information reviewed in September 2026 ranged from US$10,500–12,000 for one nominal 10 t rotating magnetic-beam listing, to US$26,000 for a published 10 t steel-bar crane, and US$135,100 for a large-span 5+5 t steel-mill magnetic-beam project. A final price requires a fully reconciled technical and commercial scope.

    Can an existing runway be reused?

    Only after rails, beams, brackets, columns, connections and foundations are checked for condition, alignment, fatigue and the new crane reactions. The magnetic beam and long-span load distribution can change wheel loads materially.

    Can the crane connect to WMS or MES?

    Yes. The interface specification defines tasks, bundle identity, coordinates, stock status, protocol, time synchronization, safety boundaries, manual override and recovery after a network interruption.

    What should be tested before handover?

    Testing covers crane motions, brakes, limits, overload protection, rotation, attachment engagement and release, representative bundles, emergency power response, placement tolerance, safety zones, interfaces and manual recovery under agreed criteria.

    Request a Rebar Handling Crane Quote

    Submit the rebar grade and surface condition, minimum and maximum bundle mass and dimensions, bar diameter, bundles per lift, tie arrangement, handling route, cycle rate, storage and vehicle drawings, span, lift, runway data, control level, power supply, destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.
    Henan Mine CraneDiscuss your requirements ↗
  • Railway Maintenance Crane Systems

    Railway Maintenance Crane Systems

    Railway Maintenance Crane Systems

    Henan Mine Crane · Depot and Maintenance Yard Lifting

    Railway Maintenance Crane Systems

    Overhead, gantry and dual-hoist crane configurations for rolling-stock depots, locomotive repair shops and outdoor maintenance yards.

    The right system starts with the maintenance task: the complete suspended load, lifting points, track-to-workstation route, building or yard support, operating duty and site acceptance requirements.

    Henan Mine Crane overhead cranes at a rail transit maintenance depot
    The Lahore Orange Line case documents lifting equipment supplied for vehicle maintenance facilities.

    SERVICE AREAS

    Depot · Workshop · Yard

    CORE EQUIPMENT

    Bridge · Gantry · Semi-gantry

    TYPICAL LOADS

    Bogie · Wheelset · Traction Unit

    FIRST DESIGN INPUT

    Lift route and full load mass

    What Is a Railway Maintenance Crane?

    A railway maintenance crane is lifting equipment selected for servicing, overhauling or assembling rail vehicles and railway assets. Inside a depot, a bridge crane moves components above a maintenance road. In an outdoor repair or storage yard, a gantry crane can serve a fixed travel corridor without relying on a roof-supported runway. A semi-gantry crane can connect a building-supported side to a ground-level rail where the layout permits.

    The term also appears in searches for self-propelled railborne cranes used for track work and accident recovery. Those machines require rail-vehicle approvals, route compatibility and on-track operating rules. The fixed overhead and gantry systems shown here are for depots and yards; they are not railborne breakdown cranes.

    Within one covered workshop, selection narrows to building runways, hook height and the component path. A depot-wide purchase also covers outdoor yards, civil works, simultaneous lifts and fleet availability.

    Plan the Lift from Vehicle to Workstation

    A crane schedule should follow each component through removal, transfer, repair and reinstallation. In a depot, a traction motor may move from a vehicle on a pit road to a service stand. A bogie may travel from a drop-table area to inspection, washing or overhaul positions. Outdoor storage or loading may need a separate gantry because the indoor bridge does not reach the yard.

    • Record vehicle type, maintenance task and approved pickup points.
    • Mark the load path across tracks, pits, doors, platforms and workstations.
    • Set the heaviest complete suspended mass, including beam and rigging.
    • Count ordinary lifts and exceptional heavy or multi-point lifts separately.
    overhead crane above a railway maintenance workshop
    Maintenance routes determine the required bridge coverage and hook approach.

    A fleet plan can use one crane type for repetitive general work and a different engineered solution for occasional long or high-consequence lifts. Do not size every bay from a single headline vehicle weight.

    Railway Maintenance Crane Selection Considerations

    Location and coverage

    Choose by where the load must move: under a roof, along a fixed outdoor track or between a building wall and yard rail.

    Complete load and lift points

    Include the component, beams, slings and clamps; obtain vehicle-maker lifting instructions for bogies or bodies.

    Structure and civil works

    Check roof or runway capacity for bridge cranes and ground rails, drainage and foundations for gantries.

    Duty and availability

    Specify lifts per shift, load spectrum, operating hours, maintenance access and the consequence of a crane being out of service.

    The procurement comparison should keep crane equipment, civil works, electrical installation, commissioning and lifting attachments as separate priced lines.

    Crane Configurations by Maintenance Location

    Maintenance location Configuration to evaluate Deciding interface
    Indoor vehicle or component bay Single- or double-girder bridge crane. Runway rail centers, roof clearance, hook approach and structural wheel loads.
    Long assembly or two-point task Double-trolley bridge crane or a specifically engineered multi-point arrangement. Individual hook ratings, combined load, synchronization and lift plan.
    Open maintenance yard Single- or double-girder gantry crane. Travel-rail route, foundations, vehicle clearances, power and wind conditions.
    Building-to-yard edge Semi-gantry crane where one side has an adequate elevated support. Wall-side runway, ground rail alignment and differential settlement.
    Track renewal or derailment response Specialist railborne or road-rail crane. Rail vehicle approvals, route limits, outriggers and recovery plan.

    Select a fixed crane from the actual service envelope. A railborne crane is a different procurement category from a depot bridge or yard gantry.

    Technical Data That Determines the Crane

    Input Specify Purchase consequence
    Capacity Maximum complete suspended mass and load distribution at each hook. Sets hoist, bridge, brakes, wheels and support reactions.
    Geometry Bridge span or gantry rail gauge, travel length, hook height and approach limits. Defines which tracks and workstations are truly served.
    Operating duty Lifts per hour, shifts, average and maximum load frequency. Changes machinery life, controls and service intervals.
    Precision Positioning requirements at pins, stands, drop pits and fixtures. May justify variable-speed motions and anti-sway controls.
    Site Electrical supply, indoor/outdoor exposure, drainage and maintenance access. Determines protection, civil work and power distribution.

    For a retrofit, an approved general arrangement should follow an actual site survey. For a new depot, send maximum wheel loads and electrical demands to the civil and building designers before they freeze the structural scheme.

    One Crane or a Depot-Wide Fleet?

    A single bridge crane may cover several adjacent work positions only when its runway reaches them, the operating routes remain clear and simultaneous maintenance demand is low enough. Multiple cranes become relevant when separate bays work at the same time or when an indoor crane cannot reach an outdoor yard.

    Estimate peak overlapping lifts by task and bay, then check whether each crane can reach pickup and landing positions without crossing an occupied road. Separate routine handling from rare bogie, carbody or recovery lifts. Availability planning should also state whether maintenance can continue while one crane is isolated for service.

    For outdoor work, compare a shared gantry travel corridor with separate local cranes. Rail crossings, road vehicles, parked rolling stock, turnouts and pedestrian access can limit a theoretically large coverage area.

    Bridge Crane, Yard Gantry or Railborne Crane?

    Bridge crane

    Best evaluated where an engineered building runway exists and the lift stays within a workshop. Leaves the floor free but transfers reactions into the structure.

    Gantry crane

    Best evaluated for a fixed outdoor maintenance route or storage/transfer area. Requires travel rails or an engineered surface and a clear path for legs.

    Railborne crane

    Used for trackside installation, infrastructure work or recovery at changing locations. Must be selected as a rail vehicle with route and operational approvals.

    A container RMG is optimized for container handling at a freight terminal. It should not be specified for bogie or machinery maintenance merely because both gantries run on ground rails.

    Bogie, Wheelset and Long-Load Attachments

    Component-specific lifting gear

    Bogies, wheelsets, traction motors and gearboxes have different centers of gravity and pickup points. The attachment must match the component and the vehicle maker’s instructions. Include lifting beams, hooks, clamps and rigging in the rated load calculation and inspection plan.

    Two-point and multi-point lifting

    A long load may need two hooks on one crane, or another engineered arrangement. Specify the rating of each hoist, maximum combined load, hook spacing, load sharing, control mode, monitoring and response to a fault. A complete carbody lift needs a vehicle-specific design and approved procedure; a standard crane’s nameplate rating is not sufficient evidence.

    Movement quality

    Low-speed hoisting and travel, predictable braking and suitable operator sightlines matter during installation onto stands and fixtures. State the required handling task in the RFQ so the control scheme can be evaluated rather than assumed.

    Runways, Ground Rails and Power

    Bridge cranes need a verified runway span, rail elevation, beam condition and available headroom. Gantry cranes need the travel-rail geometry, ground bearing or foundation design, drainage and safe separation from vehicle and pedestrian routes. Both need a power route that avoids inspection pits, door movements and maintenance access.

    At electrified facilities, define the traction-power isolation boundary and which authority controls it. Crane insulation, if separately specified, does not substitute for isolation or site electrical safety rules. Include earthing, conductor position and emergency-stop zoning in the interface review.

    multiple overhead cranes installed in railway maintenance building
    Building structure, runway rails and power routing are part of the depot lifting design.

    For a yard gantry, also establish the parked position, end stops, wind monitoring and storm-securing method appropriate to the site.

    Safe Operation and Acceptance

    The purchase specification should list overload protection, hoist and travel limits, emergency stop, buffers, alarms, braking and maintenance access. It should also state the local crane rules and railway operator procedures that apply at the destination. Load-test and acceptance arrangements must be agreed before delivery.

    Commissioning should prove travel clearances, electrical functions, braking, control modes and each special attachment. Multi-point lifts require a documented procedure, defined exclusion zone and a competent lifting team. Vehicle movement, pit access and adjacent track use must be controlled during the lift.

    Provide operators and maintainers with the approved drawings, manuals, inspection records, spare-parts list and a planned maintenance schedule for the installed system.

    Published Railway Maintenance Projects

    Lahore Orange Line depot, Pakistan

    Henan Mine Crane reports supplying 32 cranes of various types for the metro line’s operation and maintenance project. Its case states that equipment in the vehicle section and parking area supports vehicle maintenance and commissioning. The published case does not assign a capacity or crane type to each of the 32 units. View project record

    Xi’an locomotive maintenance, China

    Henan Mine Crane’s case identifies a KSQ new double-girder crane for Xi’an Railway Bureau’s high-power locomotive maintenance project, dated October 2024. The source describes the crane’s modular layout but does not publish its capacity or span. View project record

    These records establish railway-maintenance supply experience. The crane schedule for a new depot must still be built from its own vehicle fleet, lift paths and structural conditions.

    Railway Maintenance Crane Price and Project Budget

    Public 2026 supplier prices, checked on 28 September 2026, can frame an equipment budget. They describe standard industrial bridge and gantry cranes, not a completed railway maintenance facility. Every price below is in USD and must be matched to the quoted span, duty, hoist and delivery scope.

    Public 2026 equipment reference Indicative USD price Source and scope
    10 t double-girder overhead crane US$12,000–35,000 Henan Mine Crane market guide; equipment budget, delivery term not stated.
    5 t single-girder gantry, 18 m span US$11,000–17,500 Weiying Crane, 10 June 2026; equipment price reference, delivery term not stated.
    20 t double-girder gantry, 22 m span US$39,000–57,000 Weiying Crane, 10 June 2026; equipment price reference, delivery term not stated.
    10 t double-girder gantry, about 20 m span US$20,000–30,000 Voitto Crane 2026 guide; FOB factory reference from a separate supplier.

    These are market references, not Henan Mine Crane project offers. Shipping, insurance, taxes, foundations, runway or yard rails, power distribution, installation, commissioning, load testing and vehicle-specific lifting fixtures are outside or not defined in these equipment ranges. Synchronized multi-hook systems and railborne recovery cranes need separate engineered quotations. Compare supplier bids only after the same exclusions and delivery terms are shown line by line.

    Lifecycle Planning for a Maintenance Depot

    A depot crane is part of the maintenance timetable. The technical offer should therefore state inspection points, access to brakes, drives and ropes, recommended spares, fault reporting and a method to isolate one crane without disabling unrelated bays. Outdoor gantries also need a site-specific corrosion and weather-protection plan.

    For a fleet of cranes, standardizing controls and critical spare parts where technically appropriate can simplify maintenance. Ask suppliers to identify which components are common across models and which are unique to a heavy or dual-trolley unit.

    Engineering and Procurement Deliverables

    • Crane schedule by bay and yard, with rated loads, spans or rail gauges, hook heights and duty.
    • General arrangements showing lift paths, obstacles, approaches and maintenance access.
    • Maximum wheel loads, foundation or runway reactions, motor power and conductor route.
    • Control narrative, safety-device list and drawings for each special lifting attachment.
    • Factory inspection, site-test plan, manuals, spares, training and service scope.

    The facility structural engineer and railway operator should review the relevant interface documents before fabrication and installation.

    Railway Maintenance Crane RFQ Checklist

    Information to send Required detail
    Maintenance duty Vehicle types, components, maximum complete load, lifting points and lift frequency.
    Location Workshop, covered edge, yard or on-track work; mark every pickup and landing point.
    Geometry Runway span or gantry gauge, travel length, hook height, pit and track levels, obstacles.
    Site services Power supply, structural drawings, ground conditions, weather exposure and local rules.
    Commercial scope Crane only or installed package, destination, Incoterm, testing, training and spares.

    For a multi-point or whole-vehicle lift, send the vehicle manufacturer’s approved lifting information and request a separate engineered concept.

    Railway Maintenance Crane FAQ

    What crane is used for railway maintenance?

    Indoor rolling-stock maintenance commonly uses a bridge crane; a fixed outdoor service corridor may use a gantry or semi-gantry. Trackside construction and recovery use specialist railborne or road-rail equipment.

    How is a railway maintenance crane different from a rail workshop overhead crane?

    A rail workshop overhead crane is one indoor bridge-crane solution. Railway maintenance crane is a broader buying category covering depot bridges, outdoor gantries and the question of specialist on-track equipment.

    Can a gantry crane lift a railway carbody?

    Only when the vehicle lifting points, load sharing, gantry rating, attachments, ground rails and an approved lift procedure have been engineered together. A general-purpose gantry rating alone is insufficient.

    Is one crane enough for a depot?

    That depends on simultaneous lifts, runway coverage, heavy-lift frequency and whether maintenance can continue during crane service. Build a bay-by-bay task schedule before deciding fleet size.

    What should be included in a railway maintenance crane quote?

    Rated load, geometry, duty, control, attachments, wheel loads, site interfaces, testing, delivery term, exclusions and service documents should be stated explicitly.

    How much does a railway maintenance crane cost?

    Public 2026 industrial crane equipment ranges vary from thousands to tens of thousands of US dollars for common bridge and gantry configurations. A depot-ready system depends on civil works, electrical scope, lifting fixtures and installation; railborne recovery cranes are a separate quote category.

    Build the Crane Schedule Around the Maintenance Plan

    Send the bay and yard drawings, heaviest complete lifts, hook routes and operating cycle. Henan Mine Crane can prepare a site-specific equipment configuration and itemized commercial offer.

    Request a Railway Maintenance Crane Quote

    Written by: Henan Mine Crane · Technical review: source-checked product and project records · Last reviewed: 2026

    Henan Mine CraneDiscuss your requirements ↗
  • Rail Workshop Overhead Crane

    Rail Workshop Overhead Crane

    Rail Workshop Overhead Crane

    Henan Mine Crane · Rolling Stock Maintenance Lifting

    Rail Workshop Overhead Crane

    Bridge-crane systems for locomotive, metro and rolling-stock maintenance bays—selected around the actual part, lift path and workshop structure.

    Specify the complete suspended load, rail-center span, hook height over track and inspection pit, runway reactions, lift frequency and any two-point lifting method before choosing a crane model.

    Henan Mine Crane equipment at a rail transit maintenance facility
    Henan Mine Crane documents crane supply for Lahore Orange Line maintenance facilities.

    WORKSHOP USE

    Bogie, wheelset and component handling

    CRANE OPTIONS

    Single / double girder; twin trolley

    KEY SITE CHECK

    Track, pit, roof and runway clearances

    QUOTE BASIS

    Rated load + span + duty + scope

    What Is a Rail Workshop Overhead Crane?

    A rail workshop overhead crane is a bridge crane running on elevated building runways above a railway maintenance, assembly or overhaul bay. Its bridge travels along the workshop, while the hoist or trolley travels across it to move bogies, wheelsets, traction motors, gearboxes and other components between vehicles, pits and workstations.

    It is a building-mounted maintenance machine. A rail-mounted container gantry crane serves intermodal freight handling; a railway mobile crane travels to an outdoor recovery or track-work site. Neither is a direct substitute for a bridge crane inside a rolling-stock depot.

    The most suitable configuration depends on the heaviest complete lift and the handling path. A single-girder hoist can serve a light component bay; a double-girder crane is considered for heavier assemblies, higher duty or special lifting attachments. Whole-carbody lifts require a separately engineered lifting system and procedure, not an assumption based on crane capacity alone.

    Which Maintenance Tasks Must the Crane Cover?

    Map the lift from its pickup point to its landing point before setting crane travel length. In a locomotive or EMU workshop, the crane may remove a traction motor from the vehicle, carry it clear of the rail and pit, then lower it onto a maintenance stand. A bogie or wheelset route may cross several tracks and fixed service platforms.

    • Component removal and replacement above a vehicle or inspection pit.
    • Transfer from track position to bogie drop, wheelset, motor or overhaul bay.
    • Loading a service trolley or test stand without obstructing adjacent trains.
    • Occasional long or off-center loads requiring an approved lifting beam or two-point arrangement.
    overhead crane in Lahore Orange Line maintenance area
    Vehicle-maintenance and commissioning applications are reported for the Lahore Orange Line project.

    Record each load’s weight, center of gravity, pickup height, travel route, landing clearance and expected daily lift count. These facts determine hook approach, speed, control position and safe exclusion zones.

    Rail Workshop Crane Selection Considerations

    Complete suspended load

    Use the heaviest part plus slings, lifting beam, clamps and other gear below the hook; confirm whether the rated load is needed at every pickup point.

    Track-to-hook geometry

    Measure runway rail centers, rail-top level, pit depth, minimum roof clearance, bridge end approach and usable hook travel.

    Workshop structure

    Have the building engineer check runway beams, columns, bracing and foundations against final crane wheel loads and horizontal forces.

    Duty and precision

    Specify lifts per hour, shifts, load spectrum and the low-speed control needed for mating pins, bogies and sensitive assemblies.

    For a retrofit, the usable hook height and existing runway capacity often decide the viable design before a nominal tonnage does. New facilities should coordinate crane reactions with the structural designer before the building steelwork is fixed.

    Which Overhead Crane Configuration Fits the Bay?

    Configuration Appropriate workshop task What to verify before purchase
    Single-girder electric hoist Parts, tools, small wheelsets and general maintenance loads within the selected rating. Hook height, span, hoist duty, rail support and the actual attachment weight.
    Double-girder bridge crane Heavier bogies, machinery and repeated overhaul handling where trolley or duty flexibility is needed. Bridge self-weight, wheel loads, access for maintenance and lift clearances.
    Double-trolley / two-hook crane Long assemblies needing two controlled lifting points on one bridge. Combined rating, individual hook ratings, spacing, load share, synchronization and lifting procedure.
    Suspended / underhung crane Selected light-duty side bays where floor-supported runways are impractical. Roof support capacity, suspension points and hook coverage.

    Henan Mine Crane lists double-girder bridge cranes and double-trolley overhead cranes. A two-hook design is specified from the actual lifting plan; it should not be treated as an automatic approval for lifting a complete carbody.

    Technical Data to Fix Before Manufacturing

    Parameter Buyer input Why it matters
    Rated capacity Maximum complete suspended mass at the hook(s). Selects hoist, bridge, brakes and runway reactions.
    Span and runway length Runway rail center distance and required long-travel coverage. Determines bridge geometry and which workstations are reached.
    Hook height and approach Lowest pickup, highest lift, roof clear height, end and side approach. Prevents conflict with rolling stock, pits, roof and service platforms.
    Duty and motions Lifts per hour, shifts, load spectrum, hoist/cross/long travel speeds. Matches machinery and controls to real service.
    Site and electrical Voltage, frequency, indoor conditions, earthing and conductor route. Defines electrical equipment and interface to the facility.

    Catalogue capacities and spans describe available product families, not a universal railway-workshop specification. The approved general arrangement and crane-load schedule should be based on the specific bay.

    Bogie, Wheelset and Carbody Lifting

    Bogie and wheelset handling

    Select the hook and attachment around the lifting points prescribed for the actual bogie or wheelset. Check load stability, sling angles, floor stand geometry and whether the trolley can place the load clear of nearby vehicles. Controlled low-speed travel is useful when aligning a heavy assembly to pins, jigs or rail vehicles.

    Long components and two-point lifts

    A double-trolley bridge can provide two coordinated hook positions for long components. The design review must state each hoist’s rating, maximum combined load, load sharing, hook separation, controls, interlocks and response to uneven loading. If two independent cranes are proposed, the lift is a separate engineered operation with an approved plan and site controls.

    Whole carbody lifting

    Carbody lifting may require purpose-built lifting jacks, synchronized hoists or an engineered multi-point system matched to the vehicle manufacturer’s approved lift points. Crane capacity by itself does not establish that a vehicle can be lifted safely.

    Workshop Layout, Pits and Rail Interfaces

    A track-centred drawing should show rolling-stock envelope, inspection-pit edges, platforms, doors, HVAC, lighting, cable trays and any overhead electrical equipment. Confirm where personnel stand to operate the crane and whether adjacent roads remain in service during a lift.

    The crane’s span is the distance between runway-rail centers, not the overall building width. The usable hook area is smaller than the nominal bridge envelope because the trolley and end carriages have approach limits. For existing depots, survey the actual runway elevation, rail straightness and support condition rather than relying on architectural dimensions.

    rail maintenance workshop overhead lifting equipment
    Workshop geometry and operating clearances should be checked against the approved lift path.

    Where overhead line equipment is present, the depot electrical authority must define isolation, earthing, access and clearance rules for the lifting zone. An insulated crane design, where specified, does not replace electrical isolation.

    Controls and Below-the-Hook Equipment

    Variable-speed motions

    Inverter-controlled hoist and travel can improve approach to mating surfaces and reduce abrupt movement of suspended assemblies.

    Operator visibility

    Choose pendant, radio remote or cab control according to line of sight, vehicle length, service pits and pedestrian routes.

    Lifting beams and fixtures

    A beam or dedicated fixture must match the rail component’s approved lifting points and be included in total suspended mass.

    Two-hook controls

    For multi-point lifts, define common control, independent control, load monitoring and the required response to loss of synchronization.

    Ask for a control narrative and lifting-attachment drawing with the quotation when precise installation or synchronized lifting is part of the work scope.

    Safety, Inspection and Acceptance

    The technical offer should identify the applicable crane design and local acceptance requirements for the destination. The final configuration must be assessed against the railway operator’s maintenance rules and the building’s structural design. Confirm overload protection, upper/lower limits, travel limits, emergency stop, buffers, alarms, brake behavior and safe maintenance access in the approved specification.

    During installation and commissioning, verify runway geometry, electrical supply, crane travel, hoist motions, braking, controls and each project-specific attachment. Agree on factory inspection, site testing, documentation and the locally required load-test procedure before purchase. Operators also need a documented lift plan for abnormal or multi-point lifts.

    No suspended load should pass over occupied workstations. Define exclusion zones around tracks and pits, lockout for maintenance, and a method to prevent unintended movement of vehicles during lifting.

    Railway Maintenance Project Experience

    Xi’an Railway Bureau locomotive maintenance project

    Henan Mine Crane’s project record identifies a KSQ new double-girder crane for a high-power locomotive maintenance facility in Xi’an, China (October 2024). The published record describes a compact modular design and positioning characteristics. It does not disclose the installed capacity or span. View project record

    Lahore Orange Line maintenance facilities

    Henan Mine Crane reports supplying 32 cranes of various types for the Lahore Orange Line metro operation and maintenance project in Pakistan. Its case record places crane products in the vehicle section and parking area for maintenance and commissioning. It does not state that all 32 were overhead cranes or publish individual crane ratings. View project record

    These cases show experience in railway maintenance settings. A new depot still requires its own load schedule, bay drawings and approved lifting method.

    Rail Workshop Overhead Crane Price and Budget

    Public 2026 prices, checked on 28 September 2026, are a starting budget for ordinary overhead-crane equipment. A rail workshop quotation must be built from the actual crane specification and separately priced site work. The figures below are manufacturer-published market references in USD, not fixed offers for a railway maintenance installation.

    Public 2026 reference Equipment-only range Publication and commercial scope
    5 t single-girder overhead crane US$4,000–14,000 Henan Mine Crane market guide; equipment budget reference, delivery term not specified.
    10 t double-girder overhead crane US$12,000–35,000 Henan Mine Crane market guide; equipment budget reference, delivery term not specified.
    20 t double-girder overhead crane US$22,000–60,000 Henan Mine Crane market guide; equipment budget reference, delivery term not specified.
    10–20 t double-girder overhead crane US$12,000–35,000 Voitto Crane, 5 June 2026; China FOB factory guide, supplier-specific public range.

    These public ranges exclude or do not define freight, insurance, import duty, runway steel, building reinforcement, site electrification, installation, commissioning, local load testing and any bespoke lifting beam. Twin-trolley controls, synchronized lifting or a vehicle-specific fixture need a project quotation. For an installed depot budget, compare itemized crane equipment, structural works, electrical works and site services on the same scope.

    What a Technical Offer Should Include

    • General arrangement showing bridge, trolley, hook approach, clearances and runway rail centers.
    • Rated load, hoist arrangement, duty classification, speeds, motor power and maximum wheel loads.
    • Runway and power-supply interface requirements, including conductor position and electrical data.
    • Safety device list, control narrative and any two-point lifting or attachment drawings.
    • Inspection and test plan, operation and maintenance manuals, spare-parts list and site-service scope.

    For an existing building, the crane supplier’s wheel-load schedule should be reviewed by the facility structural engineer before purchase approval. For new works, exchange these interface documents before runway fabrication.

    Rail Workshop Crane RFQ Checklist

    A useful request for quotation includes a marked-up bay plan and the following inputs:

    Buyer information Detail to send
    Loads and lift points Heaviest bogie, wheelset or machine; attachments; center of gravity; any long or multi-point load.
    Bay geometry Runway rail centers and length; floor, rail and pit elevations; roof clear height; obstacles.
    Operating cycle Lifts per shift, shifts per day, load mix, desired speeds and positioning tolerance.
    Electrical and site Voltage/frequency, power route, ambient conditions, existing runway drawings and destination.
    Commercial scope Crane only or installed package; shipping term; installation, testing, training and spares.

    Where the load is a complete carbody or other special railway assembly, include the vehicle maker’s lifting instructions and ask for a specific lifting concept rather than a generic overhead-crane quote.

    Rail Workshop Overhead Crane FAQ

    What is the difference between a rail workshop overhead crane and an RMG?

    A rail workshop overhead crane runs on elevated building runways to lift rolling-stock components inside a depot. An RMG runs on ground rails across container tracks and truck lanes at a freight terminal.

    What capacity is needed for bogie maintenance?

    Capacity is set by the heaviest complete suspended bogie or component, including beams and rigging. There is no safe universal tonnage; vehicle data and the lifting method must be reviewed.

    Can one overhead crane lift a whole railway car?

    Only if a vehicle-specific, engineered lifting system and approved procedure establish the load, lifting points, synchronization, structure and controls. Rated crane capacity alone is insufficient.

    Is single or double girder better for a locomotive workshop?

    Single girder can suit lighter component handling. Double girder is considered for heavier loads, longer spans, higher duty, precise trolley requirements or multiple hooks. The building and lift geometry decide the final choice.

    How is overhead-crane span measured?

    Span is the center-to-center distance between the crane runway rails. Building width and rail-track gauge are different measurements.

    What makes a railway workshop crane quote more expensive?

    Capacity, span, duty, hook height, variable-speed control, twin trolleys, attachments, runway reinforcement, electrification and site services are major cost drivers.

    Specify a Crane Around the Maintenance Bay

    Send the workshop drawing, heaviest complete lift, required hook path and operating cycle. Henan Mine Crane can prepare a configuration and itemized quotation for the defined scope.

    Request a Rail Workshop Crane Quote

    Written by: Henan Mine Crane · Source review: linked product and project records · Last reviewed: 2026

    Henan Mine CraneDiscuss your requirements ↗
  • Precast Concrete Crane

    Precast Concrete Crane

    Precast Concrete Crane

    Henan Mine Crane · Precast Plant and Yard Lifting Systems

    Precast Concrete Crane

    Engineered overhead and gantry crane systems for demoulding, transfer, curing-area handling, yard stacking and dispatch of precast beams, slabs, wall panels, pipes and tunnel segments.

    Henan Mine Crane configures each precast concrete crane around the complete suspended load, element geometry, approved lifting points, production cycle, yard layout, operating environment and required supply boundary.

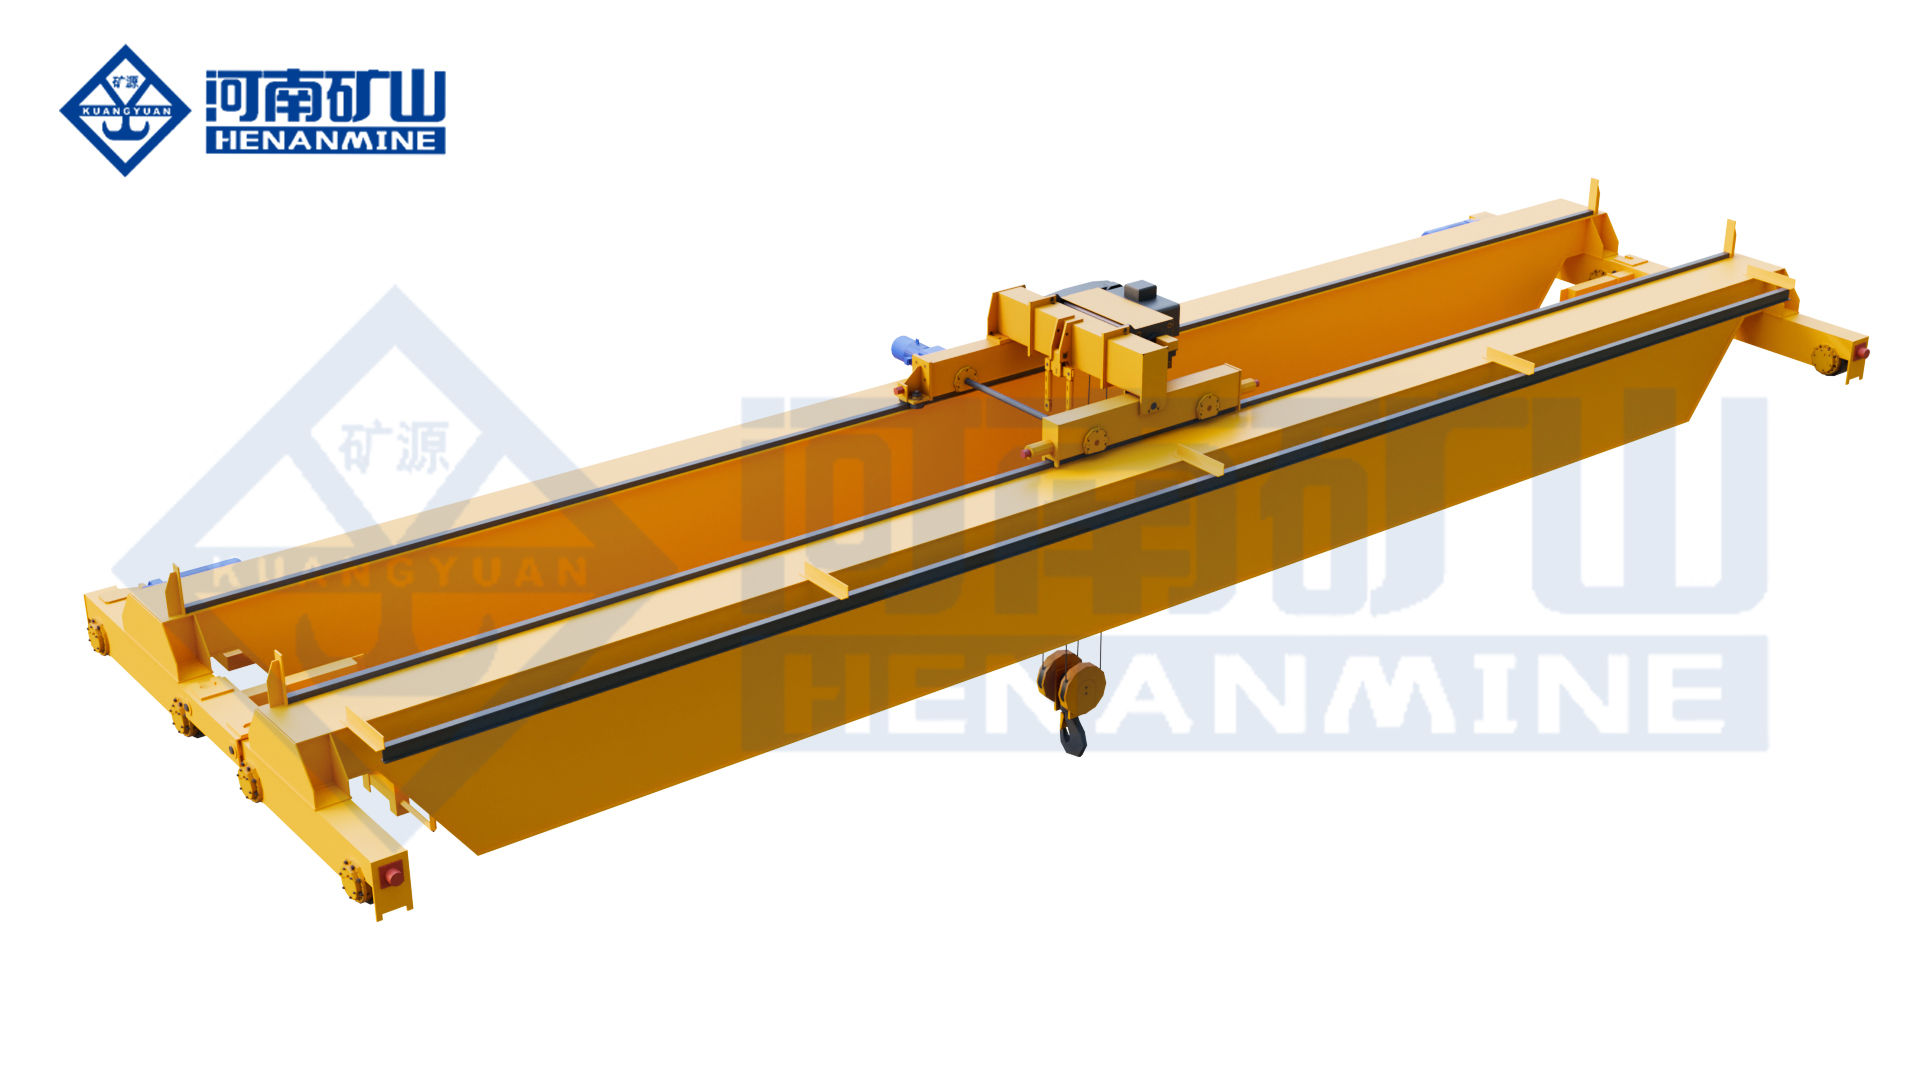
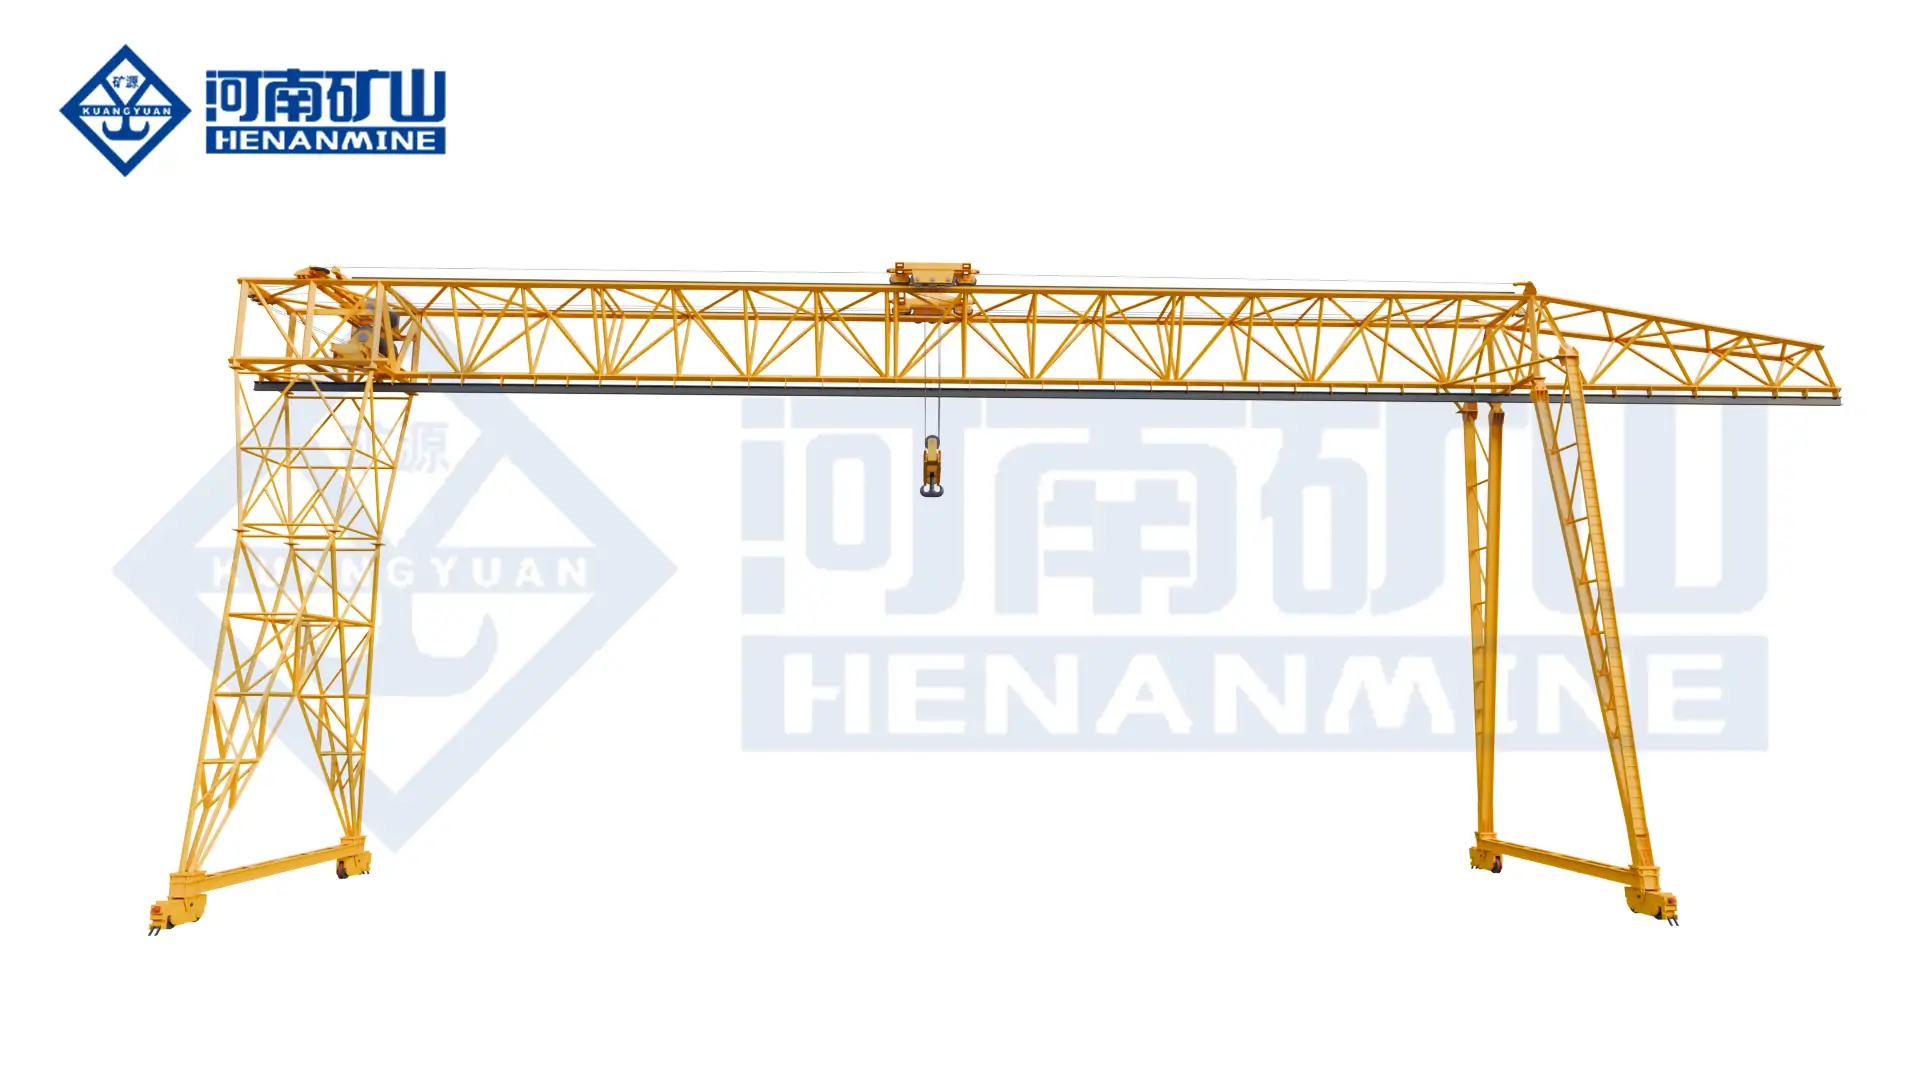
    Henan Mine Crane double-girder gantry crane adaptable to precast concrete yard handling
    The crane, lifting beam, rigging, runway and yard workflow must be engineered as one material-handling system.

    Handled products
    Beams, slabs, panels, pipes and segments

    Primary systems
    Overhead, rail-mounted and rubber-tyred cranes

    Critical inputs
    Total load, geometry, lift points and cycle rate

    Commercial basis
    Project-specific technical and price proposal

    Precast Concrete Handling from Mold to Dispatch

    A precast concrete crane supports a production and logistics sequence rather than a single lift. Typical duties include moving reinforcement cages and molds, releasing approved elements from casting beds, transferring components to finishing or curing areas, stacking finished products in the yard and loading delivery vehicles. One facility may require separate indoor and outdoor systems because the loads, travel routes and operating environments are different.

    Concrete components may be heavy, long, flexible or sensitive to edge damage. Improper sling angles, unverified lifting anchors, uncontrolled rotation or unequal loading can damage the product even when the crane remains below its rated capacity. The lifting method therefore defines the required hook arrangement, spreader beam, motion control and operator visibility.

    The element must be released for lifting under the precast producer’s approved quality procedure. Concrete strength at release, lifting-anchor capacity and permissible support locations are process and structural-engineering decisions; they are not replaced by selecting a larger crane.

    Precast Concrete Crane Configurations

    01 · Single-Girder Overhead Crane

    An economical indoor option for lighter precast elements, molds, reinforcement assemblies and general production handling where the capacity, span and duty remain within the selected hoist system.

    02 · Double-Girder Overhead Crane

    A production-bay solution for heavier elements, higher duty, greater hook height or project-defined dual-hook and double-trolley handling inside a precast factory.

    03 · Single-Girder Rail Gantry Crane

    A practical yard crane for smaller and medium precast products along defined storage or loading lanes, subject to wind, rail, wheel-load and duty verification.

    04 · Double-Girder Rail Gantry Crane

    The principal configuration for heavy beams, bridge girders, large wall panels and repeated outdoor loading where stability, span, hook coverage and long-load control are decisive.

    05 · Truss Gantry Crane

    A rail-mounted alternative for selected outdoor spans and transport constraints. Its open structure, connection details, corrosion protection and inspection access must suit the site environment.

    06 · Rubber-Tyred Gantry Crane

    A self-propelled solution for serving multiple production or storage lanes without fixed travel rails. Ground bearing, steering, braking, power source and traffic management become major design inputs.

    Compare Precast Plant and Yard Crane Options

    The correct system follows the production route, not only the maximum tonnage. Indoor overhead cranes, fixed-lane gantry cranes and mobile yard carriers solve different material-flow requirements.

    Configuration Matched duty Principal advantage Procurement constraint
    Indoor overhead crane Casting bay, demoulding, finishing and production transfer Clear floor area and full bay coverage Requires a verified building runway and support reactions
    Single-girder rail gantry Defined yard lane with moderate load and duty Lower structural complexity for suitable applications Capacity, span, headroom and duty are more limited than heavy double-girder systems
    Double-girder rail gantry Heavy beams, panels, segments and truck loading Strong load, span and multi-hook engineering flexibility Rails, foundations, storm restraints and yard alignment are part of the system
    Rubber-tyred gantry Multiple lanes, changing routes and flexible yard logistics Trackless travel between work zones Higher machine complexity; ground, steering and traffic interfaces must be controlled
    Launching gantry Erection of bridge girders at the construction alignment Purpose-designed placement at bridge spans Not a substitute for a factory production or storage-yard crane

    Select Capacity from the Complete Suspended Load

    Crane capacity must cover the governing precast element together with the lifting beam, hook block, slings, shackles, lifting clutches and other below-the-hook equipment included in the approved method. Element weight should come from controlled production data and include the agreed design tolerance.

    Long products require more than sufficient tonnage. The design must confirm centre of gravity, lifting-point spacing, permissible sling angle, allowable support conditions, deflection sensitivity and rotation control. A spreader beam may be required to keep loads at the lifting anchors within the approved directions and to prevent excessive lateral force on the concrete.

    When two hooks, two trolleys or two cranes share a load, allowable load distribution, synchronization, communication, stopping logic and the response to a drive or power fault must be engineered. Two crane nameplate capacities cannot simply be added to authorize a tandem lift.

    Match the Crane and Rigging to the Precast Product

    Precast product Handling priorities Typical crane-system considerations
    Bridge beams and girders Long-load stability, multiple lift points and controlled alignment Double-girder gantry, engineered spreader, synchronized hooks or trolleys where specified
    Wall panels and façade elements Surface protection, controlled rotation and vertical storage interfaces Smooth VFD motion, adequate hook approach, approved lifting frame and protected contact points
    Hollow-core and solid slabs Edge protection, product-specific pick points and stacking sequence Overhead or gantry crane with approved clamps, beams or lifting inserts as defined by the producer
    Pipes, manholes and culverts Roll prevention, balanced pickup and clearance through storage lanes Purpose-approved attachment, stable travel and defined set-down supports
    Tunnel segments Repetitive positioning, curved geometry and finish protection Repeatable control, segment-compatible lifting frame and production-line integration
    Molds and reinforcement cages Frequent production handling and changing load geometry Appropriate overhead crane, attachment changeover and duty based on actual cycles

    Technical Specification for a Precast Concrete Crane

    Final values are established from the element schedule, production layout, civil drawings, operating method and destination requirements. The following information forms the basis of a comparable technical proposal.

    Specification item Project definition
    Rated capacity Heaviest complete suspended load, rigging included, for each hook or operating mode
    Crane type and structure Single or double girder; overhead, rail gantry, truss gantry or rubber-tyred system
    Span and travel length Rail gauge, building bay or yard lane width, runway length, cantilever coverage and end approaches
    Lifting height Lowest pickup, highest obstacle, stack height, vehicle loading height and required safety clearance
    Hoist and hook arrangement Single hook, main and auxiliary hook, double trolley or synchronized lifting arrangement
    Duty and load spectrum Loads per hour, shifts, annual operating days, typical load distribution and expected service life
    Speeds and control Normal and low speeds, acceleration, positioning requirement, control station and automation scope
    Below-the-hook equipment Spreader beam, lifting frame, slings, clutches, approved clamps, storage stand and identification
    Runway or ground interface Rail profile, support spacing, allowable wheel loads, foundation data, ground bearing and drainage
    Environment Indoor or outdoor location, temperature, wind, rain, dust, humidity, corrosivity and altitude
    Electrical supply Voltage, phase, frequency, power-feed method and permitted voltage variation
    Codes and acceptance Destination regulations, agreed design standard, inspection plan, testing and documentation language

    Control, Safety and Outdoor Protection

    Controlled Motion

    Variable-frequency drives, suitable low-speed operation and controlled acceleration reduce shock loading and help position fragile or long elements at molds, racks and vehicles.

    Load Protection

    Overload protection, upper and lower limits, travel limits, service brakes, emergency stop and hook safety devices are specified for the selected crane and local requirements.

    Long-Load Management

    Where required, synchronized controls, load feedback, skew monitoring, anti-sway functions and defined fault responses support the approved multiple-point lifting method.

    Wind and Parking

    Outdoor cranes may require wind indication, operating limits, rail clamps, storm anchors, parking procedures, weather protection, drainage and lightning measures based on site data.

    Operator Visibility

    Pendant, radio remote or cabin control is selected from the travel route and sightlines. Cameras, lighting, warning devices and communication systems can support restricted-visibility areas.

    Restricted Lift Zone

    Traffic separation, exclusion zones, defined signaling and an approved lift plan remain essential. Crane controls do not replace the site’s safe system of work.

    The final safety functions and performance levels are defined in the approved technical specification and risk assessment for the destination and operating method.

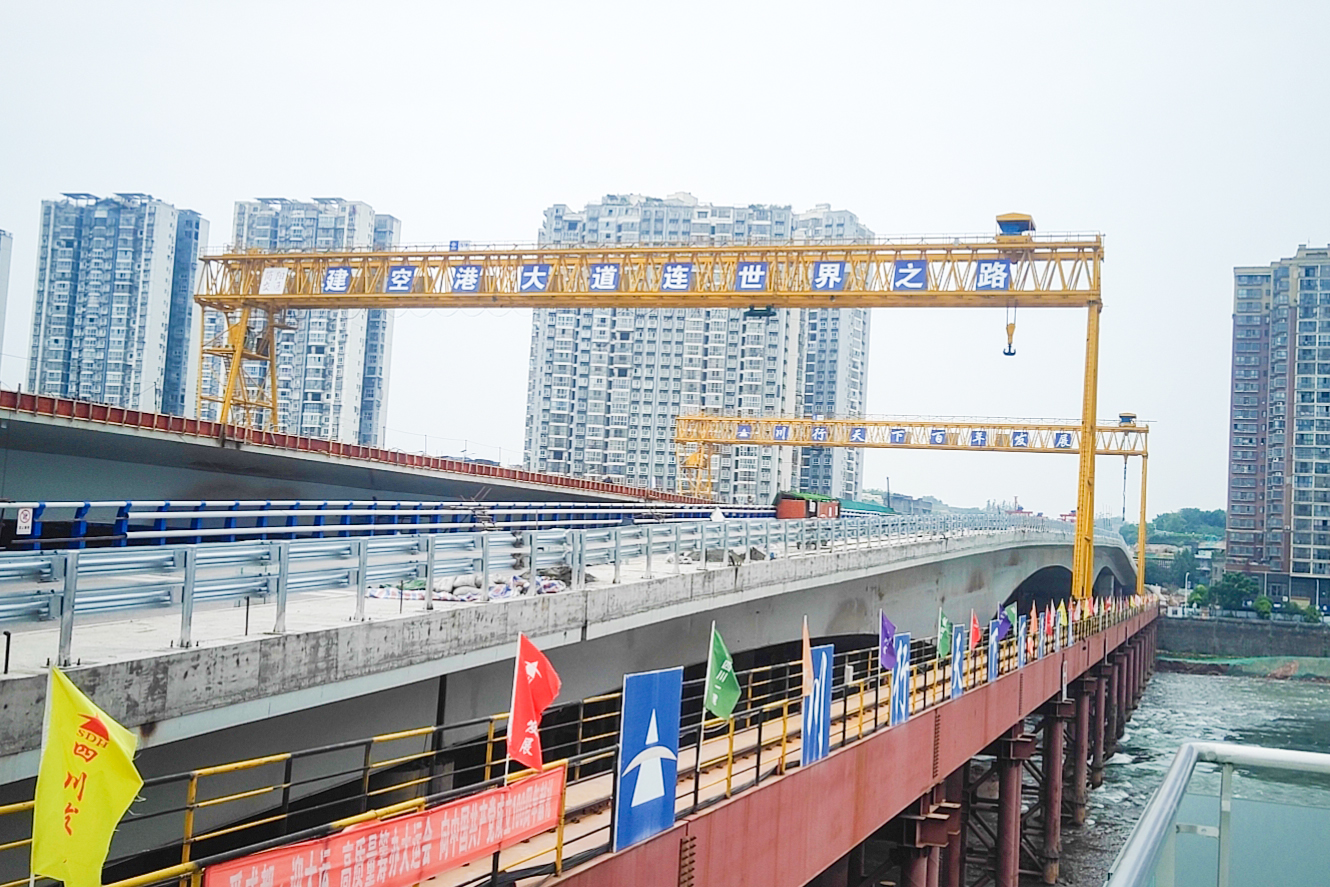
    Henan Mine Crane 75t large-span gantry crane project for long bridge components
    Verified project reference: 75t rated capacity, 72m span and 23m lifting height for large bridge-component handling.

    Related Large-Component Handling Project

    75t, 72m Large-Span Bridge Gantry Crane

    Henan Mine Crane supplied a special gantry crane with a 75t rated capacity, 72m span and 23m lifting height for the Jianzhou Bridge project. The system was designed for outdoor lifting and positioning of large steel box-girder components across a wide construction area.

    This verified project handled steel bridge components rather than precast concrete. It is relevant to precast procurement because it demonstrates engineering experience with long loads, large spans, outdoor exposure, rail and civil interfaces, controlled positioning and project-specific structural design.

    A precast concrete crane is re-engineered around concrete-element geometry, approved lifting points, rigging loads, production frequency, stacking layout and surface-protection requirements; the project parameters are not transferred without calculation.

    View Verified Project

    Engineering Deliverables and Quality Records

    A procurement-ready proposal should define the crane and every interface that affects performance, cost or acceptance. Henan Mine Crane can align the documentation package with the agreed code, inspection plan and customer responsibilities.

    Design Definition

    General arrangement, hook coverage, wheel loads, clearances, power demand, control philosophy and below-the-hook interfaces.

    Manufacturing Control

    Material traceability, dimensional inspection, welding and non-destructive examination records can be defined where required by the contract.

    Testing and Handover

    Factory test records, electrical documentation, installation instructions, site-test procedures, manuals, spare-parts list and training scope.

    Henan Mine Crane publishes its production and testing capabilities. The project inspection and documentation matrix should still be agreed before manufacturing begins so that quotation and acceptance boundaries remain consistent.

    Installation, Commissioning and Maintenance Planning

    Civil Readiness

    Confirm runway alignment, rail level, foundations, wheel-load capacity, drainage, earthing, access and erection areas before crane delivery.

    Site Acceptance

    Define installation inspection, no-load and functional tests, proof-load arrangements, synchronized-mode checks and operator training in the contract.

    Lifecycle Availability

    Plan brake, rope, hook, wheel, rail, gearbox and electrical inspections around production shifts; establish critical spares before handover.

    For operating plants, installation must be coordinated with casting schedules, storage capacity and truck-dispatch requirements. For new facilities, crane wheel loads, clearances and power supply should be frozen before the building or yard civil design is finalized.

    Precast Concrete Crane Price and Supply Scope

    Public-market figures reviewed in September 2026 indicate a wide equipment-only budget of approximately US$10,000 to US$280,000+ for conventional precast overhead and rail-mounted gantry systems. Within that broad market, standard double-girder indoor systems are commonly indicated around US$28,000–US$95,000, while conventional outdoor double-girder gantry equipment is often indicated around US$18,000–US$120,000. Basic listings may appear below these levels, but they frequently omit the runway, special lifting beam, freight, installation, testing or destination compliance.

    These figures are planning bands, not a Henan Mine Crane quotation. Heavy long-span cranes, double-trolley systems, high-duty process cranes and self-propelled rubber-tyred machines may exceed the ranges. A valid comparison requires every supplier to price the same performance and delivery boundary.

    Commercial package Items to define before price comparison
    Crane equipment Structure, trolley or hoist, hooks, drives, electrics, controls, access and safety devices
    Precast lifting equipment Spreader beam, lifting frame, slings, clutches or approved clamps, stands and sensors
    Runway and civil interface Rails, foundations, conductor system, embedded parts, storm anchors and structural checks
    Logistics and installation Packing, inland delivery, ocean freight, insurance, lifting equipment, erection and supervision
    Testing and support Commissioning, test weights, third-party inspection, documentation, training, spares and warranty boundary

    Capacity, span, lifting height, duty, number of hooks, speed control, automation, outdoor protection, steel-market conditions, destination and Incoterm materially affect the final price. The quotation should state currency, validity, inclusions, exclusions and site responsibilities.

    Precast Concrete Crane RFQ Information

    Submit the element schedule and maximum complete suspended load; product dimensions and centres of gravity; approved lifting points; rigging concept; casting, curing, stacking and dispatch layout; required span, lift height and travel length; duty cycles; indoor or outdoor environment; runway or ground data; power supply; destination; applicable standard; project schedule; and required freight, installation, testing and training scope.

    Send Project Requirements
    A technical configuration and itemized commercial scope can then be prepared on a consistent design basis.

    Frequently Asked Questions

    What crane is used in a precast concrete plant?

    Indoor production commonly uses single- or double-girder overhead cranes. Outdoor storage and loading commonly use rail-mounted gantry cranes, while rubber-tyred cranes suit yards that require travel between multiple lanes.

    How is precast crane capacity selected?

    Capacity is based on the heaviest element plus the hook block, lifting beam, slings, shackles, lifting clutches and other suspended equipment. The approved lifting method and load distribution must also be verified.

    Is a double-girder crane necessary for concrete beams?

    It is often selected for heavy or long beams, greater spans, higher duty or multi-hook handling. A single-girder crane may remain suitable when the verified load, span, headroom and operating cycle are within its design envelope.

    Can one crane handle both production and outdoor storage?

    Only if the physical route and crane structure provide continuous coverage. Most facilities use separate indoor and yard cranes because buildings, weather exposure, travel paths and stacking duties differ.

    When is a rubber-tyred gantry crane suitable?

    It suits yards that need one machine to serve multiple lanes or changing routes without fixed rails. Ground bearing, grade, turning space, steering mode, braking and mixed-traffic controls must be assessed.

    Can two cranes lift one precast beam?

    A tandem lift is possible only under an engineered method that defines load sharing, crane capacities, controls, communication, travel, fault response and supervision. Independent cranes should not be paired by assumption.

    What lifting device is used for precast concrete?

    The device follows the product engineer’s approved lifting points and may include a spreader beam, lifting frame, slings, clutches or purpose-approved clamps. Sling angle and attachment loads require verification.

    What protection is required for an outdoor precast yard crane?

    The site specification may require suitable coatings, weather-protected electrics, drainage, wind monitoring, rail clamps, storm anchors, lightning protection and low-temperature measures.

    How much does a precast concrete crane cost?

    Conventional equipment-only public budgets may range from about US$10,000 to US$280,000+, but a valid quote requires capacity, span, height, duty, hook arrangement, rigging, runway, controls, delivery and installation scope.

    What information is needed for a fast quotation?

    Provide element weights and dimensions, lift points, rigging, site layout, span, height, travel length, cycle rate, environment, runway or ground details, voltage, destination, schedule and required supply boundary.

    Technical content record

    Prepared by Henan Mine Crane Technical Sales · Technically reviewed by Crane Engineering · Last reviewed September 2026

    Related Precast Concrete Crane Products

    Henan Mine Crane double-girder gantry crane for heavy precast yard service

    Double-Girder Gantry Crane

    Heavy rail-mounted configuration for beams, panels and repeated outdoor handling.

    View Details →

    Henan Mine Crane single-girder gantry crane for precast yard handling

    Single-Girder Gantry Crane

    Cost-conscious yard option for suitable moderate loads, spans and operating cycles.

    View Details →

    Henan Mine Crane double-girder overhead crane for precast production bays

    Double-Girder Overhead Crane

    Indoor production crane for heavier components, frequent duty and engineered multi-hook lifts.

    View Details →

    Henan Mine Crane double-girder truss gantry crane for outdoor yards

    Double-Girder Truss Gantry Crane

    Open-structure rail gantry option for selected outdoor spans and project logistics.

    View Details →

    Henan Mine Crane rubber-tyred gantry crane for flexible precast yard routes

    Rubber-Tyred Gantry Crane

    Trackless mobile configuration for serving multiple yard lanes and work zones.

    View Details →

    Precast Lifting Proposal

    Request a Precast Concrete Crane Quote

    Share the element schedule, complete suspended load, lifting points, factory or yard layout, required coverage, operating cycle, environment, destination and delivery scope. Henan Mine Crane will develop a defined crane configuration and commercial proposal for the precast operation.

    Henan Mine CraneDiscuss your requirements ↗
  • Power Plant Crane

    Power Plant Crane

    Power Plant Crane

    Henan Mine Crane · Power Generation Lifting

    Power Plant Crane

    Engineered overhead crane systems for turbine-generator installation, powerhouse maintenance and supporting material handling across power-generation facilities.

    From a high-capacity turbine-hall bridge crane to a smaller service-bay hoist, Henan Mine Crane selects each configuration around the heaviest approved lift, building geometry, operational life and plant-specific environment.

    Henan Mine Crane double-girder bridge crane shown in a thermal power plant application
    The turbine-hall crane is specified for the generating-unit lifting plan and the facility’s future maintenance requirements.

    Core application
    Generating-unit erection and scheduled maintenance

    Main structure
    Project-rated overhead crane and runway interface

    Control selection
    Defined slow-speed handling, braking and positioning

    Commercial approach
    Scope-based technical and price proposal

    A Power Plant Needs More Than One Lifting Specification

    The main turbine hall must accommodate high-value generators, turbine components, casings and related equipment during initial erection and later overhauls. A power plant crane in this zone is normally a bridge crane selected from the approved lift study, with the required main-hook capacity, potential auxiliary hook, building coverage and controlled motion.

    Other plant zones have different duty. A coal or biomass handling area may need a grab rather than a hook. A mill maintenance bay may need cross-bay access or a compact hoist. A waste-to-energy bunker requires a dedicated high-cycle feed arrangement. Treating all these jobs as one model would produce an incomplete technical and commercial specification.

    Henan Mine Crane can configure separate lifting packages for the turbine hall, auxiliary maintenance areas and suitable bulk-material operations, with a defined interface to the power-station structure and installation schedule.

    Power Plant Crane Configurations

    01 · Turbine-Hall Bridge Crane

    A heavy-duty double-girder configuration for approved turbine-generator erection loads and major maintenance lifts.

    02 · Main and Auxiliary Hooks

    Two separately rated hook functions where the lift plan calls for high-capacity lifts and smaller service operations.

    03 · Auxiliary-Bay Crane

    An appropriately rated bridge crane or electric-hoist solution for workshop, pump, valve or other service-bay loads.

    04 · Track-Switching Access

    A project-specific cross-travel arrangement for designated maintenance routes between compatible track sections.

    05 · Coal or Biomass Grab

    A grab crane for approved loose fuel handling, sized for material properties and actual handling cycles.

    06 · Ash and Slag Handling

    A separate bulk-handling design for the temperature, dust, abrasiveness and operating frequency of the ash area.

    07 · Hydropower Powerhouse Crane

    A generating-unit lifting arrangement developed around turbine, generator and maintenance access in the powerhouse.

    08 · Retrofit or Upgrade

    A replacement study that checks existing runway reactions, hook reach, electrical supply and construction access.

    Power Plant Crane Compared with Other Lifting Configurations

    The equipment must fit its actual lifting duty. A compact electric-hoist bridge crane, for example, is not a direct substitute for a heavy turbine-hall erection crane.

    Crane arrangement Typical task Selection basis Main limitation
    Heavy double-girder bridge Turbine and generator erection Full suspended load, reach and runway capacity Greater building and installation interface
    Electric-hoist bridge Auxiliary maintenance and service bays Local loads, frequency and headroom Not inherently suitable for major-unit erection
    Cross-travel bridge Selected inter-bay maintenance routes Track geometry and safe transfers Requires a designed track-switch interface
    Grab overhead crane Fuel, ash or other loose materials Grab payload, throughput and environment Not a replacement for a hook-type turbine lift

    Engineer the Heaviest Lift and the Everyday Overhaul

    The main hook rating starts with the heaviest approved component, but the suspended weight also includes the lifting beam, slings, shackles and any other below-the-hook equipment. The component’s centre of gravity, certified lifting points and necessary clearances determine how it can be raised and transferred.

    A second design check covers planned maintenance after commissioning: turbine-casing removal, rotor handling, generator work, pump replacement and laydown routes. Hook coverage at both ends of the hall can be as important as rated tonnage. The turbine supplier’s maintenance procedure should be reconciled with the crane’s hook approach and usable lifting height.

    If two cranes or two trolleys will handle one load, the lifting sequence, load sharing, controls and structural reactions require a separate engineered plan. Two nameplate capacities must never simply be added to define an allowable tandem lift.

    Lift Envelope Check

    Maximum component and rigging weight

    Component dimensions and lifting points

    Lowest required hook position

    Highest transfer elevation

    End approach and side approach

    Laydown area and approved travel route

    Technical Specification for a Power Plant Crane

    Every project value is established from turbine supplier drawings, the EPC lifting plan and the station’s maintenance strategy. Installed power-generation capacity, measured in MW, is not the crane’s lifting capacity, measured in tonnes.

    Project parameter Information required to define the crane
    Main lifting capacity Heaviest component plus lifting beam, slings and accessories
    Auxiliary hook Required secondary loads, service tasks and independent rating
    Span and runway Rail gauge, runway length, rail-top elevation and permitted wheel reactions
    Lifting height Hook and load path above equipment, foundations and obstacles
    Hook approaches Coverage at generator, turbine, service platforms and laydown zones
    Duty and speeds Construction lifts, overhaul frequency, load spectrum and low-speed handling
    Controls and protection Operator station, speed control, brakes, limits and emergency functions
    Environment Actual heat, dust, humidity, corrosion and electrical area classification
    Delivery interface Site power, access, erection window, testing requirements and destination

    Controlled Motion, Safety and Plant Conditions

    Low-Speed Positioning

    Hoist and travel drives can be specified for smooth acceleration and a defined slow-speed range as equipment approaches its final position. Acceptance criteria should state the required operating behavior rather than promising an unverified positioning tolerance.

    Protection and Interlocks

    Overload protection, upper and lower limits, end-of-travel controls, emergency stop, braking and safe operation near other cranes are reviewed against the actual crane design and applicable project requirements.

    Dust, Heat and Humidity

    Electrical enclosure protection, cable routing, paint system and service access are selected for measured conditions. Explosion-protected equipment is considered only where a documented hazardous-area classification requires it.

    For nuclear applications, safety classification and project-specific regulatory requirements must be established separately. A conventional thermal-power turbine-hall crane must not be presented as a nuclear-qualified lifting system.

    Power Plant Project · Xinjiang, China

    Generator Stator Lift at a 2 × 350 MW Cogeneration Project

    Henan Mine Crane supplied lifting equipment for a 2 × 350 MW cogeneration project in Jimsar, Xinjiang. During construction, the project crane supported the lift of the Unit 1 generator stator—a critical generating-unit installation task.

    The crane solution incorporates full variable-frequency speed control and PLC-based control for regulated motion, with equipment selected for the site’s heat and dust. The 2 × 350 MW designation describes the plant’s generating output, not the crane’s lifting rating; the latter is defined by the approved lift plan.

    This installation illustrates why the crane, rigging, generator delivery sequence and building clearances must be coordinated before the heavy lift. The project lift path and the station’s subsequent maintenance needs both belong in the original technical specification.

    View the Xinjiang Power Plant Project

    Henan Mine Crane power plant project lifting equipment at the Jimsar cogeneration facility
    Project photograph from Henan Mine Crane’s Jimsar 2 × 350 MW cogeneration installation.

    Overseas Project · Indonesia

    Two 120 t Turbine-Hall Cranes for a Thermal Power Project

    At a thermal power project in Morowali, Central Sulawesi, Henan Mine Crane supplied two double-girder overhead cranes for the construction of three 380 MW generating units. The cranes are described with 120 t main and 30 t auxiliary hook ratings and are used for major unit installation and future maintenance access.

    The project demonstrates a defined main-and-auxiliary-hook arrangement for heavy erection and smaller support lifts. Its ratings are project-specific; a new station’s crane cannot be selected solely from a previous plant’s 120 t marking or the output of its generating units.

    Explore the Thermal Power Crane Application

    Project Data

    Location: Morowali, Central Sulawesi

    Supply: two double-girder overhead cranes

    Hook marking: 120 t main / 30 t auxiliary

    Plant: three 380 MW thermal generating units

    Installation, Acceptance and Long-Term Support

    Building Interface

    Check runway geometry, support reactions, end clearances, lifting access and the stage at which the crane can be assembled inside the turbine hall.

    Testing and Handover

    Agree on factory inspection, site commissioning, load tests, protection checks, manuals and operator instruction under the applicable project standard.

    Lifecycle Maintenance

    Specify inspectable brakes, ropes, wheels, electrics and service platforms; define spare parts and the maintenance plan before the first scheduled outage.

    The purchase schedule should identify when the crane is needed for generator-unit erection, not just when the entire facility is commissioned. Crane delivery, runway completion and load testing are therefore coordinated with the EPC construction milestones.

    Power Plant Crane Price and Supply Scope

    There is no dependable single list price for a power plant crane. Online figures for general workshop bridges, individual hoists or loosely specified high-capacity cranes do not establish the price of a turbine-hall system with approved rigging loads, auxiliary lifting, control requirements and site installation.

    Henan Mine Crane quotes against a defined technical scope. To compare offers on a like-for-like basis, the commercial schedule should identify the following separately:

    Crane and hoists
    Bridge, main and auxiliary hooks, drives, controls and designed duty.

    Civil interface
    Runway, power feed, support checks and any structural modification.

    Project execution
    Inspection, packing, shipping, erection, commissioning and load testing.

    After handover
    Documentation, operator training, warranty boundaries and initial spares.

    Price changes with the heaviest approved load, crane span, lift height, precision-control functions, environmental protection, location and delivery terms. Each quotation should state its currency, Incoterm, validity, exclusions and responsibilities for site work.

    Power Plant Crane RFQ Information

    Supply the turbine-hall and runway drawings, generating-unit component lift list, maximum load including rigging, hook approach targets, lift height, building clearance, erection sequence, expected maintenance lifts, site power, environmental conditions, destination and required acceptance standard. Include the turbine supplier’s lifting instructions where available.

    Send Project RequirementsThe crane configuration and commercial quotation can then be developed against the same lift plan.

    Frequently Asked Questions

    What crane is used in a turbine hall?

    A double-girder overhead crane is commonly specified for heavy turbine and generator erection and future overhaul work. Its final ratings, hook configuration and bridge geometry depend on the approved lift plan.

    How is power plant crane capacity selected?

    Assess the heaviest approved component plus lifting beam and rigging, then check its handling path and site requirements. A generating unit’s MW rating is not an overhead crane capacity.

    What is the auxiliary hook for?

    A separately rated auxiliary hook can handle smaller components, approved rigging operations and some maintenance lifts. Its use with the main hook must be governed by the crane design and lift plan.

    Can an electric-hoist bridge crane replace a turbine-hall crane?

    Not automatically. An electric-hoist bridge may suit a service bay or other defined loads, while main generating-unit erection may require a different lifting mechanism, capacity, hook approach and structural rating.

    Why are hook approach and lifting height important?

    A crane must reach the turbine, generator and service areas while lifting the rigged component clear of foundations, platforms and pipework. A correct tonnage without sufficient reach may still be unusable.

    Can two cranes lift one component together?

    Only under an engineered tandem-lift arrangement that defines load sharing, coordinated control, rigging and runway reactions. Adding the two rated capacities does not establish a permitted combined load.

    Is a grab crane appropriate for all power plant areas?

    No. Grabs are for suitable bulk fuel, ash or other loose materials. Turbine-generator equipment requires approved hooks and rigging; a waste-to-energy feed bunker requires its own application-specific grab system.

    Does every power plant crane need explosion protection?

    No. Electrical protection is selected according to a documented area classification and the applicable local requirements. Heat and dust alone do not justify assigning a universal explosion-proof rating.

    What determines the price of a turbine-hall crane?

    Hook ratings, span, lifting height, control requirements, duty, plant environment, runway interface, testing and delivery scope. A detailed technical offer is necessary for a meaningful price comparison.

    Can a crane be installed in an existing power station?

    A replacement or retrofit is possible subject to runway capacity, remaining hook travel, power supply, access openings and the construction window available without disrupting operations.

    Related Power Plant Crane Products

    Thermal Power Bridge Crane

    Heavy turbine-generator installation and planned maintenance applications.

    Electric-Hoist Double-Girder Crane

    A separate option for appropriately rated power-station service bays.

    Cross-Travel Overhead Crane

    Track-switching access for engineered power-plant maintenance routes.

    Single-Girder Service Crane

    Smaller maintenance loads where its rating and duty are suitable.

    Grab Double-Girder Overhead Crane

    Bulk fuel or approved loose-material applications, not turbine lifts.

    Power Plant Lifting Proposal

    Request a Power Plant Crane Quote

    Share the power-station lift study, turbine-hall drawings, heaviest component and rigging weights, required hook coverage, environmental conditions and project destination. Henan Mine Crane will develop a defined crane configuration and commercial scope for the generating facility.

    Henan Mine CraneDiscuss your requirements ↗
  • Port Crane Manufacturers

    Port Crane Manufacturers

    Port Crane Manufacturers

    Henan Mine Crane · Port and Terminal Equipment

    Port Crane Manufacturers

    Port crane procurement requires a manufacturer capable of matching the equipment to vessel dimensions, cargo flow, quay strength, yard layout, operating duty and the terminal’s maintenance resources. Henan Mine Crane develops configurable ship-to-shore cranes, portal harbor cranes, rail-mounted gantry cranes, rubber-tyred gantry cranes and container straddle carriers for coastal and inland terminals.

    Equipment selection is only one part of the contract. A complete proposal defines the lifting arrangement, power and control interfaces, wind and corrosion protection, testing, delivery, installation, training and spare-parts scope.

    ship-to-shore container crane at a port terminal
    Ship-to-shore crane geometry is established from vessel profile, berth layout and the required container-handling cycle.
    CARGOContainers · Bulk · General Cargo
    TERMINAL ZONEQuay · Yard · Intermodal
    DESIGN BASISSite and Cargo Data
    COMMERCIAL BASISDefined Project Scope

    Port Crane Systems for Terminal Operations

    The term port crane manufacturer covers several different equipment families. An STS crane transfers containers between vessel and quay. A portal harbor crane handles bulk or general cargo across a working radius. RMG and RTG cranes stack containers in the yard; a straddle carrier transfers and stacks containers across terminal routes. These systems are complementary rather than interchangeable.

    The choice starts with cargo type, vessel and berth dimensions, annual throughput, peak-hour demand, yard stacking plan and intermodal connections. Selecting a crane from rated capacity alone can leave insufficient outreach, poor wheel-load compatibility or a mismatch between quay discharge and yard capacity.

    Selection Considerations

    Cargo and Handling Device

    Confirm container dimensions and maximum gross mass, or bulk density, grab payload, general-cargo dimensions and lifting points.

    Vessel and Berth

    Specify beam, container rows, deck and hatch elevations, tidal range, berth length and required front and back reach.

    Quay and Ground

    Confirm rail gauge, wheel-load limits, existing foundations, apron width, pavement bearing and drainage.

    Throughput and Duty

    Define annual and peak volumes, shifts, operating cycles, required availability and maintenance windows.

    Yard Configuration

    State rows, stacking height, truck lanes, turning areas, rail tracks and future block expansion.

    Wind and Marine Exposure

    Provide operating and storm wind criteria, salt exposure, ambient range and coating requirements.

    Power and Automation

    Identify utility supply, diesel or electric strategy, cable routing, TOS interfaces and control mode.

    Delivery Boundary

    Define crane, spreader or grab, freight, site assembly, commissioning, load testing, training and spares.

    Port Crane Types Compared

    The following equipment families serve different stages of the cargo route. Published ranges on individual product pages are preliminary and must be checked against the project specification.

    Equipment Operating Zone Typical Cargo Decisive Interface
    Ship-to-Shore Crane Quayside Containers Vessel reach, quay reactions and spreader capacity
    Portal Harbor Crane Quay and multipurpose berth Bulk, breakbulk and project cargo Working radius, grab or hook and marine protection
    Rail-Mounted Gantry Crane Fixed yard block or rail terminal Containers Rails, foundations, span and stacking plan
    Rubber-Tyred Gantry Crane Flexible yard blocks Containers Pavement, steering, power and block transfer
    Container Straddle Carrier Yard transfer and stacking Containers Travel routes, turning, stacking and fleet planning

    Quayside Crane Engineering

    portal harbor crane for bulk and general cargo quayside handling
    Portal crane radius, vessel clearance and cargo attachment are engineered as a single working envelope.

    STS Container Handling

    Outreach is set by vessel beam and furthest container row; lift above and below rail follows vessel and tidal extremes. Capacity must identify whether it is under spreader or includes spreader mass. Wheel loads, rail gauge, backreach and boom parking position are checked against the quay.

    Portal Harbor Operations

    Portal cranes require lifting capacity across a specified radius chart, not a single headline capacity. Bulk grab cycles, hook loads and container attachments impose different duty and control requirements.

    Wind and Marine Conditions

    Operating and out-of-service wind criteria, storm anchoring, protective coatings, access routes and maintainable electrical enclosures are included in the technical agreement.

    Container Yard Crane Engineering

    RMG: Defined Rail Corridor

    A fixed rail corridor supports repeatable container handling in high-density blocks and intermodal yards. Rail alignment, wheel reactions, span, cantilevers and truck or rail interfaces must be coordinated before civil construction.

    RTG: Flexible Yard Blocks

    Tyred travel permits movement between yard blocks subject to route width and ground condition. Diesel, hybrid, battery and busbar-assisted configurations differ in infrastructure, operating cost and emissions.

    Shared Selection Basis

    State container rows, stacking height, truck lanes, spreader specification, hoisting and travel speeds, anti-sway requirement, terminal operating system interface and desired fleet availability.

    rail-mounted container gantry crane for an intermodal terminal
    An RMG crane follows a defined rail corridor and requires coordinated yard, rail and power infrastructure.

    Manufacturer Evaluation and Technical Documentation

    Design Evidence

    General arrangement, load chart, wheel reactions, duty basis, structural calculations and wind criteria should match the tender.

    Manufacturing Controls

    Review the proposed inspection plan for steelwork, welding, drives, electrics, coating and factory functional tests.

    Acceptance Criteria

    FAT, site commissioning, load testing, spreader or grab tests and performance demonstrations need contractual pass criteria.

    Lifecycle Support

    Manuals, electrical drawings, parts lists, training, service access and spare-part lead times influence terminal uptime.

    Applicable structural, crane, electrical, maritime and local regulatory requirements are stated in the contract. Certificates or compliance claims are assessed against the exact crane configuration and destination jurisdiction.

    40.5 Tonne RMG Application: Inland Port Handling

    40.5 tonne rail mounted gantry crane application for inland port container handling
    Rail-mounted gantry configuration for container transfer between yard and intermodal handling routes.

    The 40.5 tonne inland-port RMG application sets out a rail-mounted container-handling configuration for dry ports, rail freight areas and intermodal logistics hubs.

    The engineering configuration addresses container specification, handling route, rail geometry, electrical controls and spreader compatibility. Final duty, span, height, interfaces and acceptance criteria depend on terminal-specific data.

    For procurement, the defining interfaces are the rail corridor, container stack envelope and connections to truck and rail handling areas. These details should be reconciled with terminal drawings before freezing the crane general arrangement.

    Installation, Commissioning and Maintenance

    Site Readiness

    Verify quay or yard bearing capacity, rail survey, erection access, lifting plan, power interface and storm-protection foundations.

    Commissioning

    Electrical, brake, limit, interlock and wind-protection checks precede load testing, operating trials and operator training.

    Planned Maintenance

    Structural connections, ropes, brakes, wheels, tyres, spreaders, corrosion protection, cable systems and safety devices require duty-based inspection.

    Port Crane Price and Total Project Cost

    There is no defensible single price for a port crane. Public supplier indications for smaller or simpler container RTG equipment begin at approximately USD 700,000–1.2 million. Larger, electrified or automated units may cost substantially more. These market indications are not Henan Mine Crane quotations and do not establish a comparable price for STS, portal harbor or RMG cranes.

    A commercial evaluation compares equivalent capacity, reach or span, duty, spreader or grab, drive and power technology, controls, wind and corrosion requirements, supply terms and acceptance criteria. STS and portal equipment require an engineered quotation after vessel and quay data are reviewed.

    Crane Equipment

    Structure, machinery, spreader or grab, electrical systems and controls.

    Terminal Infrastructure

    Rails, quay strengthening, pavement, power distribution and communications.

    Delivery and Service

    Freight, insurance, import costs, erection, testing, training and spares.

    Quotation Data

    Cargo type · maximum load under spreader or hook · vessel dimensions · required outreach and lift · quay and rail data · yard layout · annual and peak throughput · duty · wind and corrosion criteria · site power · control and TOS interface · destination port · delivery and site-work scope.

    Port Crane Procurement FAQ

    Which crane handles containers at the berth?

    A ship-to-shore crane is designed for vessel-to-quay container transfer; reach and lift follow vessel and water-level data.

    Which crane is suitable for bulk cargo?

    A grab-equipped portal harbor crane can serve berth handling where outreach, grab payload and tonnes-per-hour duty are established.

    What is the difference between RTG and RMG?

    RTG cranes travel on tyres and may move between blocks; RMG cranes travel on fixed rails within a defined handling corridor.

    How is STS outreach determined?

    The furthest container row, vessel beam, mooring offset and berth layout establish minimum working outreach.

    Does lifting capacity include the spreader?

    Capacity basis must state whether the rating is under spreader or includes spreader and attachment mass.

    Can port cranes connect to terminal software?

    Control interfaces can be specified for a terminal operating system when protocols, safety permissions and acceptance tests are defined.

    How is storm protection specified?

    Operating and parked wind cases govern brakes, clamps, anchors, tie-downs and terminal procedures.

    Does equipment price include installation?

    Not automatically. Freight, civil work, rails, erection, commissioning and testing must be explicitly included or excluded.

    What documents support supplier evaluation?

    General arrangement, load chart, wheel reactions, duty basis, inspection plan, electrical architecture, test plan and spare-parts schedule.

    What information is required for a port crane quote?

    Cargo, vessel profile, berth and yard plans, required output, operating duty, wind criteria, power, destination and supply scope.

    Related Port Crane Products

    Ship-to-Shore Crane

    Quayside handling for container vessels.

    Portal Harbor Crane

    Berth-side lifting for bulk and general cargo.

    RMG Container Crane

    Fixed-rail container yard and intermodal operations.

    RTG Container Crane

    Flexible tyre-mounted yard stacking.

    Container Straddle Carrier

    Terminal container transfer and stacking.

    Port Crane Product Range

    Compare the complete quay and yard equipment range.

    Terminal Equipment Proposal

    Request a Port Crane Quote

    Submit cargo data, vessel profile, berth or yard drawings, required throughput, operating duty, power supply, wind criteria, installation location and project scope. Henan Mine Crane will prepare an equipment configuration and commercial proposal from the confirmed terminal requirements.

    Henan Mine CraneDiscuss your requirements ↗
  • Plate Mill Crane Systems

    Plate Mill Crane Systems

    Plate Mill Crane Systems

    Henan Mine Crane · Process Lifting Systems for Plate Mills

    Plate Mill Crane Systems

    Heavy-duty overhead cranes for slab receiving, furnace and mill-area transfer, roll change, plate handling, finishing, stacking, storage and dispatch.

    Henan Mine Crane engineers each plate mill crane around the actual material route, gross suspended load, plate dimensions and temperature, handling attachment, operating duty, runway interface, production controls and maintenance strategy. The resulting proposal can cover an individual process crane or a coordinated fleet across the rolling and finished-plate areas.

    double girder plate mill crane operating in a hot rolled steel plant
    A double-girder process crane provides controlled material handling across a hot-rolling and steel-plate production bay.

    PRIMARY ARCHITECTURE

    Top-Running Double Girder

    LOAD ATTACHMENTS

    Hook, Clamp, Magnet or Beam

    OPERATING PROFILE

    Process-Defined Heavy Duty

    CONTROL OPTIONS

    Cabin, Radio, PLC & Automation

    What Is a Plate Mill Crane?

    A plate mill crane is an overhead process crane configured for the production and internal logistics of steel plate. It may handle hot or cold slabs, work rolls, mill equipment, lifting beams, magnets, clamps, finished plates or plate packs. The term identifies the production environment; it does not describe one universal crane model.

    The correct crane depends on its process zone. A slab-yard crane must control long, heavy and sometimes hot feedstock. A mill-maintenance crane needs accurate low-speed positioning for roll and equipment changes. A finishing or warehouse crane must lift plates without uncontrolled bending, surface damage or accidental pickup of additional layers. One facility can therefore require several crane configurations with different capacities, duties, attachments and control philosophies.

    Plate mill cranes are different from ladle cranes. Ladle cranes are engineered for molten-metal handling and its specific redundancy and risk controls. They are also different from coil-handling cranes, which use C-hooks, coil grabs or other devices designed around a cylindrical load. A plate mill project should identify the material form and production step before the crane type is selected.

    Henan Mine Crane supplies hot-rolling mill bridge cranes, slab handling cranes, rotating electromagnetic beam cranes and automated plate-handling systems as separate engineered platforms.

    Where Cranes Work in a Plate Mill

    Crane scope should follow the plate flow from incoming slab to dispatch. Separating the work by process zone prevents a maintenance crane, production crane and warehouse crane from being specified as if they perform the same task.

    Slab Receiving and Buffer Storage

    Unload, identify, stack and retrieve slabs by grade, heat or rolling schedule. Clamp, magnet or lifting-beam selection depends on slab temperature, dimensions, surface scale, stack arrangement and traceability requirements.

    Furnace and Mill-Line Transfer

    Move feedstock or process components near reheating and rolling equipment. Radiant heat, scale, restricted access, collision zones and production interlocks become part of the crane design basis.

    Roll Change and Mill Maintenance

    Lift work rolls, backup rolls, chocks, drive components and maintenance tools. Low-speed control, hook approach, lift height, rigging clearance and reliable inching are often more important than high travel speed.

    Finishing and Inspection

    Transfer plates between cooling, leveling, cutting, inspection, marking and repair stations. The attachment must support the plate without excessive deflection, marking or unintended multi-sheet pickup.

    Finished-Plate Warehouse

    Stack and retrieve individual plates or packs by order, grade and size. Position feedback, inventory interfaces, stack-height control and automated scheduling can reduce search time and handling damage.

    Dispatch and Loading

    Load rail wagons, trucks or internal transfer vehicles. Side approach, outdoor exposure, vehicle-clearance zoning, communication with ground personnel and the required loading sequence govern the configuration.

    A process map should record every pickup point, placement point, load state, handling frequency, travel distance, traffic conflict and upstream or downstream interlock. This is the basis for deciding whether the mill needs one versatile crane, dedicated zone cranes or a coordinated fleet.

    For plant-wide planning, the steel mill crane system should separate molten-metal, slab, billet, plate, coil, scrap, roll-change and general-maintenance duties.

    automatic plate mill crane transferring steel plates
    Plate-handling equipment is selected around material geometry, temperature, surface condition, stack logic and production flow.

    Components and Operating Principle

    A plate mill crane normally uses a top-running bridge with an open-winch trolley or another process-duty lifting mechanism. The hoist raises the load and attachment, the trolley crosses the bay and the bridge travels along the runway. Drives, brakes and controls coordinate these motions so the load can be picked, transported and placed within the required tolerance.

    Bridge and End Carriages

    Box girders, diaphragms, end carriages, wheels and travel drives carry vertical, lateral, acceleration and skew forces. Span, duty, fatigue spectrum, wheel loads and runway stiffness govern the structure.

    Open-Winch Trolley

    Drum, wire rope, sheaves, reducer, motor, service brake and specified emergency or redundant braking form the lifting mechanism. The reeving and rope fleet angle are engineered for the attachment and lift path.

    Load Attachment

    Hooks, slab clamps, plate clamps, fixed or rotating magnet beams, vacuum lifters and mechanical beams address different materials. Attachment mass is included in the gross suspended load.

    Electrification and Protection

    Runway power, trolley festoon or energy chain, panels, VFDs, motors, encoders and cables are selected for temperature, scale, dust, vibration, maintenance access and the declared enclosure level.

    Control and Position Feedback

    Cabin, radio or PLC control can combine encoders, anti-sway, cameras, laser or barcode identification, load measurement, zoning and production-system interfaces.

    Runway Interface

    Rails, clips, runway beams, columns, brackets and foundations receive crane reactions. Maximum and minimum wheel loads, transverse forces and longitudinal forces are issued for structural coordination.

    Plate Mill Crane Selection Considerations

    Selection begins with the material and process consequence, not nominal capacity alone. The operating data below should be fixed before a technical quotation is compared.

    01 · Gross Suspended Load

    Include the heaviest slab, plate, roll or component plus clamp, magnet, beam, hook block, slings and every below-hook item. State normal and maximum load cases.

    02 · Material Geometry and Stack

    Provide minimum and maximum length, width, thickness, mass, flatness, center of gravity, bundle form, support points, stack height and gaps between layers.

    03 · Temperature and Surface

    Declare material temperature, radiant heat, scale, oil, water, paint, surface quality and permitted contact marks. These factors can change magnet, clamp and vacuum performance.

    04 · Duty and Production Cycle

    Define lifts per hour, shifts, annual hours, load spectrum, travel distances, acceleration, waiting time and the production effect of a crane outage.

    05 · Attachment and Retention

    State whether the crane lifts one plate, a plate pack, a slab, a roll or maintenance equipment. Define power-loss behavior, locking, pickup confirmation and load-release control.

    06 · Geometry and Runway

    Confirm span, runway length, rail elevation, lift height, hook approaches, maintenance clearances, existing rail data, building reactions and installation access.

    07 · Motion and Automation

    Specify full and creep speeds, acceleration, positioning tolerance, anti-sway, synchronized motion, inventory tracking, MES/WMS interface and manual recovery mode.

    08 · Reliability and Project Boundary

    Define required redundancy, maintainability, critical spares, runway and electrification scope, freight, erection, testing, training, local inspection and performance acceptance.

    Plate Mill Crane Configurations Compared

    The handling device is part of the crane system. Its mass, load path, power supply, retention method, rotation and control logic must be included in the equipment specification.

    Configuration Primary Load Operating Advantage Critical Selection Point Relevant Henan Mine Crane Platform
    Heavy-duty hook crane Rolls, chocks, mill components, maintenance loads and rigged plate bundles Flexible use with conventional lifting beams, slings and project-specific tools Rigging time, safe access and load control may limit high-cycle production handling Double-Girder Bridge Crane
    Slab clamp crane Hot or ambient slabs within an approved thickness and width range Positive mechanical engagement and efficient slab-yard stacking Clamp geometry, locking, contact pressure, slab temperature and pickup confirmation Slab Handling Crane
    Fixed electromagnetic beam crane Ferromagnetic plates, billets, profiles and selected plate packs Fast pickup without manual slinging and distributed support along long material Steel grade, temperature, thickness, air gaps, scale, stack count and power-loss retention Electromagnetic Bridge Crane
    Rotating electromagnetic beam crane Long plates and profiles that must change orientation Aligns loads with stacks, vehicles or production lines without rotating the crane bridge Rotation envelope, anti-sway, cable routing, stops, load clearance and orientation feedback Electromagnetic Hanging Crane
    Vacuum plate lifter crane Individual flat plates with compatible, sufficiently clean surfaces Useful where magnetic pickup is unsuitable or surface contact must be distributed Surface porosity, scale, oil, temperature, sealing, reserve vacuum and loss-of-power response Engineered attachment with a compatible process crane
    Automated plate handling crane Slabs, plates or plate packs within a controlled product and storage envelope Repeatable positioning, inventory tracking, task scheduling and reduced manual traffic Data quality, obstacle detection, fail-safe logic, exception recovery and production interfaces Automatic Steel Plate Handling Crane

    A changeable attachment can increase flexibility, but changeover time, storage stands, connector design, control-mode selection and proof of correct engagement must be included. A single multi-purpose crane is not automatically more reliable or economical than dedicated process cranes.

    Plate Mill Crane Technical Specification Framework

    Henan Mine Crane maintains several steel-plate and slab-handling platforms. The published positions below support preliminary configuration; they are not guaranteed combinations. Final capacity, span, lift, working class, speeds, wheel loads, attachment and controls are confirmed on the approved technical schedule.

    Product Platform Published Capacity Position Published Span Position Published Lift Position Published Working Class Typical Plate-Mill Role
    Hot-rolling mill specialized bridge crane 50–200 t 13–35 m Up to 26 m in the published position A6 published; final duty by process Heavy production handling, roll or tooling service and hot-rolling workshop duties
    Slab handling crane 20–150 t 10–39 m 5–23 m A7–A8 published Continuous-casting transfer, slab yard, buffer storage and furnace-feed logistics
    Rotating electromagnetic hanging-beam crane 5–50 t 10.5–31.5 m 6–20 m A6–A7 published Finished plate, profile and long-product handling where load rotation is required
    Electromagnetic bridge crane 5–32 t including attachment in the published product position 10.5–31.5 m 6–30 m Project-defined within the published family Plate, billet, profile and ferromagnetic material transfer
    Automatic steel plate handling crane 0.5–100 t in the published solution position Project-defined Project-defined A5–A7 published Automated stacking, retrieval, line feeding, warehouse transfer and dispatch

    Specification rule: attachment capacity, crane rated load, structural duty and mechanism duty are separate entries. A published maximum from one product family should not be combined with another product family’s maximum span, lift or speed unless the engineered offer confirms that combination.

    Plate, Slab and Roll Handling Attachments

    Attachment selection determines how force enters the load. Long plate can deflect, thin plate can peel from a magnetic stack, hot scale can create an air gap, and a clamp can damage edges or surfaces if its contact geometry is wrong. Testing must therefore use representative materials, temperatures and stack conditions rather than a nominal dead weight alone.

    The approved design records the full range of material properties and the unacceptable conditions. Operators and automation logic need a clear permissive for correct pickup, a defined response to incomplete engagement and a controlled release sequence.

    rotating electromagnetic beam attachment for plate mill crane
    A rotating magnet beam can distribute lifting points along long plate and change its orientation within the approved clearance envelope.
    Attachment Data Required Retention and Confirmation Typical Restriction
    Electromagnet Steel grade, thickness, temperature, air gap, surface scale, plate count, magnet layout and center of gravity Current monitoring, pickup permissive, backup power or other approved retention strategy, audible/visual status and controlled release Performance changes with temperature, alloy, surface gaps and unintended multi-sheet attraction
    Mechanical slab or plate clamp Thickness and width range, edge condition, temperature, coefficient of friction, contact-pressure limit and permitted pickup faces Positive locking, open/closed indication, load confirmation and release prevention while suspended Contact damage, variable geometry and misaligned pickup must be evaluated
    Vacuum lifter Surface flatness, roughness, porosity, coating, contamination, temperature, pad arrangement and allowable deflection Independent circuits where required, reserve capacity, vacuum monitoring, low-vacuum alarm and release interlock Hot, heavily scaled, warped or leaking surfaces can make vacuum unsuitable
    Hook, beam and sling system Lifting points, sling angle, beam self-weight, plate support spacing, center of gravity and rigging access Hook latch or approved connection, proof-tested beam, identified rigging and controlled lift plan Manual rigging time and personnel exposure may conflict with production-cycle targets

    Heat, Scale, Dust and Runway Conditions

    Plate mills combine thermal exposure, abrasive scale, vibration, frequent reversing and long runway travel. Environmental controls should be based on measured or specified conditions at the crane components, not furnace or material temperature alone.

    Thermal Survey

    Record ambient temperature, radiant-heat intensity, exposure duration, hot-material path and ventilation. Shields, component separation, insulation and cooling are then assigned where required.

    Scale and Dust Control

    Enclosures, seals, filtered ventilation and accessible cleaning points protect panels, brakes, motors, encoders and bearings. Accumulation zones should not obstruct cooling or inspection.

    Runway Geometry

    Rail gauge, elevation, straightness, joints, clips and support settlement affect skewing and wheel wear. Existing runways require survey and structural verification before crane manufacture.

    Wheel and Rail Interface

    Wheel diameter, flange geometry, hardness, rail section, bearing arrangement and drive balance are coordinated with duty, wheel loads and runway alignment.

    Cabin Environment

    Visibility, glazing protection, filtration, cooling or heating, seat ergonomics, access, escape route and camera coverage are defined for the operator’s actual exposure and sight lines.

    Outdoor and Coastal Areas

    Dispatch yards may require wind monitoring, storm parking, rain protection, corrosion category, drainage, lightning protection and weather-dependent operating limits.

    Controls, Safety Functions and Automation

    Safety functions are selected from the risk assessment, applicable code and process consequence. Automation can improve repeatability, but it also requires defined equipment states, protected operating zones, verified sensor coverage and a controlled recovery method.

    Function Purpose Specification Detail Acceptance Evidence
    Variable-frequency motion control Smooth acceleration, controlled stopping and creep positioning Full speed, minimum stable speed, ramp time, braking sequence and load-dependent settings Recorded motion tests under defined load cases
    Overload, limits and braking Prevent overload and motion beyond the approved envelope Rated load limiter, upper/lower limits, travel limits, overspeed protection and braking architecture Set-point records and functional test results
    Attachment permissive Confirm correct magnet, clamp, vacuum or beam engagement before transport Sensor voting, minimum retention state, alarm, inhibited motions and controlled release conditions Normal and fault-condition test matrix
    Anti-collision and protected zones Separate cranes, structures, mill equipment, vehicles and restricted areas Slowdown and stop distances, sensor coverage, blind zones, bypass authority and reset logic Zone map and witnessed approach tests
    Positioning and anti-sway Support repeatable pickup, stacking and machine-interface movements Coordinate system, target tolerance, load dependence, calibration and fallback mode Repeatability trials at representative stations
    MES/WMS and inventory interface Exchange tasks, product identity, storage location and completion status Protocol, data ownership, time synchronization, task arbitration, cybersecurity and offline recovery Interface simulation and integrated production trial

    Design Basis, Inspection and Acceptance

    The contract should identify one coherent design and safety basis. Standards are not interchangeable line by line, and a CE, ISO, FEM, CMAA or ASME reference does not replace a project-specific compliance matrix. Local statutory requirements remain applicable at the installation site.

    Possible International Design Basis

    A project may specify the ISO 4301 classification framework with relevant crane standards, the EN 13001 series with EN 15011 for bridge and gantry cranes, or a North American basis using CMAA specifications and applicable ASME B30 requirements. The purchase specification states the selected route.

    Engineering Deliverables

    General arrangement, wheel loads and reactions, design calculations where contracted, duty classification, mechanism data, attachment calculations, electrical drawings, control narrative, interface list and maintenance-access plan.

    Manufacturing Inspection

    Material identification, welding procedure and welder qualification, dimensional inspection, specified nondestructive examination, wheel and rail-interface checks, assembly verification, coating records and electrical-panel inspection.

    FAT and Site Acceptance

    Factory testing verifies accessible functions before shipment. Site acceptance then checks runway, erection, alignment, electrical protection, no-load operation, load testing, attachment behavior, interfaces, training and handover against agreed criteria.

    Plate Mill and Slab Handling Project Experience

    Relevant experience is evaluated by process similarity: material form, temperature, duty, attachment, automation, runway span and production consequence. Two Henan Mine Crane references illustrate the difference between a coordinated mill fleet and a dedicated slab-handling crane.

    Henan Mine Crane hot rolling mill crane project

    Intelligent Hot-Rolling Mill Project

    34-Crane Fleet for Chongqing Panhua Plate

    Henan Mine Crane supplied 34 double-girder overhead cranes rated from 10 t to 100 t for production, roll handling, tooling, equipment service and maintenance across a 4.5-million-tonne steel plate facility.

    The project demonstrates why a plate mill is normally planned as a crane fleet. Capacity and controls are assigned by station instead of forcing every duty into one oversized common model.

    View Hot-Rolling Crane Solution

    50 plus 50 tonne slab clamp crane for steel plant

    High-Temperature Slab Handling Project

    50+50t Slab Clamp Crane for Shandong Iron & Steel

    The crane uses an electrically adjustable slab clamp with digital speed control, guidance, PLC monitoring, weighing, fault display and positioning functions for high-temperature steel-material handling.

    The reference is relevant where slab geometry, heat exposure, heavy duty and accurate placement require a dedicated clamp crane rather than a general hook bridge.

    View 50+50t Slab Crane Project

    Project verification: final crane selection still requires the new plant’s process data. A reference proves experience with comparable engineering problems; it does not make the reference crane an automatic fit for another runway, load spectrum or automation system.

    Engineering, Manufacturing, Installation and Handover

    A plate mill crane project moves through controlled design and acceptance stages. Process inputs are frozen before the bridge, trolley, attachment, runway reactions and interfaces are released for manufacture.

    Stage Main Activity Approval Output Procurement Control
    1 · Process definition Confirm material route, loads, temperatures, cycles, attachment and production interfaces Design-basis and duty schedule Open assumptions and excluded operating cases listed
    2 · Interface engineering Coordinate runway, clearances, wheel loads, power, controls, data and maintenance access Approved general arrangement and interface list Building and civil responsibilities assigned
    3 · Detailed design Finalize structure, mechanisms, attachment, protection, controls and safety functions Approved drawings, component schedule and control narrative Deviation register closed before production release
    4 · Manufacture and inspection Fabricate, assemble and inspect to the agreed inspection and test plan Material, weld, dimensional, coating and component records Witness and hold points identified in advance
    5 · FAT, packing and shipment Test available functions, preserve equipment, identify shipping splits and pack for the agreed route FAT record, packing list, marks and shipment release Incoterm, transport envelope and site unloading plan confirmed
    6 · Erection, SAT and training Verify runway, assemble, align, commission, load test, integrate and train Site test report, settings, punch-list closure and handover package Test weights, labor, permits and inspection authority assigned contractually

    Plate Mill Crane Price and Budget Scope

    A plate mill crane does not have a responsible fixed price without capacity, span, lift, duty, attachment, temperature, control level, runway scope and destination. Public listings can show the scale of variation, but they do not establish the installed cost of a process crane.

    Public Market Signal Checked in September 2026 Published Position What It Indicates Why It Is Not a Plate Mill Project Price
    Eurocrane DQ 50 t double-girder price guide Approximately US$9,800–110,000 on a supplier price guide Capacity alone permits a very wide commercial range Duty, span, open-winch trolley, heat protection, attachment, automation and site scope are not normalized
    Alibaba 50 t double-girder marketplace listing Approximately US$45,500–45,700 A platform offer can provide a mid-range equipment signal The listed machine is not confirmed for plate-mill duty, attachment, runway, delivery or commissioning
    Made-in-China 10+10 t steel-mill double-bridge listing US$5,000–100,000 published range Steel-mill labels still cover materially different specifications The range is too broad for capital approval and does not define process performance
    Made-in-China lower-rotating electromagnetic bridge crane listing Approximately US$208,930 A rotating magnet system can be priced far above a basic bridge crane Capacity, span, duty, magnet arrangement, controls and commercial boundary still require confirmation
    Engineered plate mill process crane Project quotation Price is built from an approved technical and supply scope Only the completed specification defines comparable value and contract risk

    Budget drivers: rated load and attachment mass; span and lift; working class and load spectrum; hoisting architecture; plate or slab temperature; magnet, clamp or vacuum package; redundant functions; positioning and automation; cabin and heat protection; runway and electrification; export packing and freight; erection, testing and local compliance.

    The named public sources were checked in September 2026 for budget context. The published figures are market observations, not Henan Mine Crane offers or endorsements. Marketplace prices can be placeholders or equipment-only values and should not be used for contract comparison without a line-by-line scope reconciliation.

    Plate Mill Crane RFQ Information

    A complete enquiry allows capacity, duty, attachment, runway reactions, electrical load and commercial scope to be priced on the same basis. Drawings, plate schedules, process layouts and photographs can be submitted with the data below.

    Material and Attachment Data

    Material type and grade; individual or pack handling; minimum and maximum mass, length, width and thickness; temperature; surface condition; stack arrangement; center of gravity; attachment preference; permitted contact marks; lifting points.

    Process and Duty Data

    Pickup and placement stations; cycle sequence; lifts per hour; shifts; annual operating hours; load spectrum; travel distance; required speeds; creep speed; outage consequence; shared or dedicated crane; future production increase.

    Building and Runway Data

    Span between rail centers; runway length; rail section; rail elevation; required lift; end and side approaches; roof and machine clearances; existing wheel-load limits; runway drawings; alignment survey; erection and maintenance access.

    Controls, Site and Commercial Data

    Cabin, radio or automatic operation; positioning tolerance; MES/WMS protocol; anti-collision zones; voltage and frequency; ambient and radiant heat; dust; destination; design standard; Incoterm; installation scope; inspection authority; documentation language.

    Frequently Asked Questions

    How is plate mill crane capacity calculated?

    Capacity starts with the maximum gross suspended load: material plus magnet, clamp, vacuum lifter, lifting beam, hook block, slings and every other item below the hoist. Load distribution, dynamic effects, duty and the selected design standard are then applied.

    Is a magnet or clamp better for steel plate?

    Neither is universally better. Magnets offer rapid non-rigged pickup of compatible ferromagnetic material. Clamps provide mechanical engagement within an approved geometry. Steel grade, plate thickness, temperature, surface, stack count, damage limits and power-loss response determine the choice.

    Can a plate mill crane handle hot slabs or plates?

    Yes, when the maximum material temperature, radiant exposure and handling duration are declared. The attachment, wire ropes, cables, sensors, panels, motors, brakes, cabin and structural shielding are then selected or protected for the actual exposure.

    Can one crane handle slabs, plates, rolls and maintenance loads?

    A multi-purpose crane is possible when capacity, duty, attachment changeover, controls and clearance support every task. High-cycle production and precision maintenance often justify separate cranes because sharing can create scheduling conflict, unnecessary complexity and a larger outage consequence.

    How much does a plate mill crane cost?

    The price is project-specific. Public listings reviewed in September 2026 ranged from tens of thousands of US dollars for generic double-girder equipment to about US$208,930 for one lower-rotating electromagnetic bridge-crane listing. A contract price requires the complete process and supply scope.

    Can a new crane use the existing plate mill runway?

    Only after the rails, beams, columns, brackets, connections and foundations are checked for condition, alignment, fatigue and new crane reactions. The crane design must remain within verified structural limits or the runway must be strengthened.

    Can the crane connect to MES or warehouse software?

    Yes. The interface specification defines task messages, product identity, locations, status feedback, protocol, time synchronization, data ownership, safety boundaries, cybersecurity, manual override and recovery after a network or system interruption.

    What documents are needed for final handover?

    The agreed package can include approved drawings, wheel-load data, manuals, component schedules, electrical diagrams, software backups, settings, inspection and test records, certificates, spare-parts lists, training records and site load-test or commissioning reports.

    Request a Plate Mill Crane Quote

    Submit the material schedule, maximum gross load, plate or slab temperature, attachment requirement, process cycle, span, lift, runway information, control level, power supply, destination and required supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.
    Henan Mine CraneDiscuss your requirements ↗
  • Pickling Line Crane Systems

    Pickling Line Crane Systems

    Pickling Line Crane Systems

    Henan Mine Crane · Engineered Coil Transfer for Pickling Operations

    Pickling Line Crane Systems

    Process-duty overhead cranes for hot-rolled coil receiving, pickling-line entry feeding, exit-coil removal, buffer storage, inspection, rework and dispatch.

    Henan Mine Crane engineers each pickling line crane around the maximum gross suspended load, complete coil envelope, line throughput, pickup and placement interfaces, acid-mist exposure, selected attachment, runway restrictions, control architecture and required operating availability.

    heavy-duty bridge crane platform for pickling line coil handling
    A process-duty bridge crane can be configured with a C-hook, powered coil tong, inside-diameter lifter or a validated magnetic system.

    PRIMARY SERVICE

    Entry, Exit & Buffer Coils

    TYPICAL ARCHITECTURE

    Top-Running Double Girder

    ATTACHMENT OPTIONS

    C-Hook, Tong, Mandrel or Magnet

    CONTROL LEVELS

    Manual, Assisted or Automatic

    What Is a Pickling Line Crane?

    A pickling line crane is a coil-handling overhead crane serving the receiving, entry, exit and storage areas of a steel strip pickling line. It unloads incoming hot-rolled coils, feeds entry saddles or coil cars, removes pickled coils from the recoiling section, transfers coils through buffers and inspection stations, and loads finished material for the next process or dispatch.

    The term does not normally describe a crane carrying steel strip through the acid tanks. During production, strip is continuously transported by the line itself through scale breaking, pickling, rinsing and drying equipment. Crane duties are concentrated around coil logistics and planned maintenance, where controlled handling directly affects line availability and coil condition.

    Pickling areas combine high cycle demand with a potentially corrosive atmosphere. Acid chemistry, mist concentration, humidity, condensation, ventilation, washdown practices and distance from the process determine the required protection. A generic outdoor coating or a higher IP rating alone does not establish suitability for acid-mist service.

    Henan Mine Crane configures pickling-line systems from double-girder bridge crane and metallurgical bridge crane platforms, combined with a project-specific attachment, corrosion-control package, positioning system and line interface.

    Pickling Line Coil-Handling Map

    A practical crane specification starts with every pickup, travel and placement point. The following zones commonly require separate operating rules even when one crane spans several functions.

    1. Incoming Coil Receiving

    Unload hot-rolled coils from trucks, rail wagons or transfer cars and place them on identified saddles. Vehicle envelope, coil eye orientation, lashing removal, edge protection and pedestrian exclusion are included in the lift plan.

    2. Entry Section Feeding

    Select the scheduled coil and place it on the entry saddle, coil car or pay-off reel interface. Low-speed approach, confirmed centerline, uncoiler availability and attachment-release permissives protect both coil and line equipment.

    3. Process-Section Maintenance

    Support planned lifting of rolls, pumps, motors, covers and other maintainable assemblies. Maintenance loads, access openings and lifting points are documented separately from routine coil-handling duty.

    4. Exit Coil Removal

    Remove the completed pickled coil from the exit saddle, recoiler coil car or turnstile only after the line confirms a safe transfer state. Coil bands, tail condition and stable support are verified before travel begins.

    5. Buffer, Inspection and Rework

    Route coils by grade, order and process status. Storage coordinates, hold areas, inspection stands and rework queues require positive identification and controlled placement on approved supports.

    6. Downstream Transfer or Dispatch

    Feed a tandem mill, annealing line, coating line or slitter, or load coils into road and rail transport. Order verification and stable final placement close the material-tracking transaction.

    One Line Can Require More Than One Crane

    Entry and exit bays can have different coil conditions, cycle requirements and environmental exposure. Independent cranes can isolate production logistics, maintenance and dispatch traffic, while overlapping coverage or an emergency transfer plan can support availability.

    The handling study records crane-to-crane collision zones, shared runway sections, handover saddles, recovery positions and the production consequence of each single failure.

    steel production bay considered during pickling line crane planning
    Bay geometry, line equipment, vehicle lanes, saddles and maintenance access define the usable crane envelope.

    Pickling Line Crane System Architecture

    Bridge and End Carriages

    Girders, wheels and travel drives are engineered from span, fatigue spectrum, wheel loads, lateral forces, runway stiffness and required approach. Walkways and service platforms support safe inspection.

    Process-Duty Hoist

    Drum, rope, sheaves, reducer, motor and brakes are sized for the gross suspended load, lift, speed, starts per hour, operating class and required redundancy or emergency lowering philosophy.

    Coil Attachment

    A C-hook, powered tong, inside-diameter lifter or approved magnet engages the defined coil range. Contact surfaces, engagement confirmation and attachment parking stands form part of the system.

    Motion and Positioning

    Variable-frequency drives provide controlled acceleration and creep speed. Encoders, laser positioning, anti-sway functions and load-height feedback support repeatable line and saddle approaches.

    Electrical and Control System

    Panels, PLC, drives, sensors, communications and operator stations are protected for the mapped environment. Diagnostics identify permissive status, faults, maintenance needs and task progress.

    Line and Inventory Interface

    Handshakes with the line PLC, coil cars, uncoiler, recoiler, turnstile, gates and storage management prevent conflicting movements and preserve coil identity.

    double girder steel mill crane platform for pickling line service
    The complete handling system includes the crane, attachment, runway, saddles, process interfaces, safety zones and recovery method.

    Pickling Line Crane Selection Considerations

    Nominal coil mass is only one selection input. The crane, attachment and controls are specified from the complete operating envelope and the consequences of delayed or failed transfer.

    Coil Envelope

    Minimum and maximum coil mass, outside diameter, inside diameter, face width, eye orientation, center-of-gravity range, winding tightness, banding, tail condition and permitted contact areas.

    Material Condition

    Steel grade, surface scale before pickling, oil or residual moisture after pickling, edge sensitivity, surface-marking limits, temperature and any restrictions on magnetic lifting.

    Throughput and Duty

    Coils per hour, lifts per shift, loaded travel distance, average and maximum load, production schedule, queuing allowance, annual hours, maintenance windows and outage consequence.

    Station Interfaces

    Saddle geometry, coil-car stroke, uncoiler and recoiler centerlines, turnstile positions, truck or rail clearances, obstacles, approach distances and attachment release conditions.

    Environment Map

    Acid chemistry and concentration, mist distribution, chloride or sulfate exposure, temperature, humidity, condensation, washdown, ventilation, dust and the location of cleaner service zones.

    Building and Utilities

    Span, lift, runway elevation, rail section, wheel-load limits, end approaches, headroom, power supply, cable route, maintenance access, erection opening and future line modifications.

    Selection rule: crane rated capacity is based on the maximum gross suspended load, including the coil, C-hook or other attachment, hook block and every component carried below the hoist. The rated load is then checked against duty, dynamic effects and the governing design standard.

    Pickling Line Crane Configurations Compared

    The appropriate arrangement follows the duty and process interface. No single configuration is optimal for every pickling line.

    Configuration Typical Service Principal Advantages Engineering Checks
    Double-Girder Crane with C-Hook Receiving, manual entry feeding, exit removal and buffer storage Mechanically simple attachment, visible engagement and comparatively straightforward maintenance Accessible coil bore, hook throat and counterweight clearance, lining, rotation, stable orientation and manual engagement time
    Double-Girder Crane with Powered Coil Tong High-cycle line feeding, automatic buffers and mixed coil widths Powered engagement, sensor feedback and stronger automation potential Jaw range, contact pressure, fail-safe retention, coil width tolerance, mechanism protection and recovery after loss of power
    Crane with Inside-Diameter Lifter Defined coil bores and applications requiring limited outer-surface contact Positive internal engagement and compact outer profile Bore strength, ID range, insertion depth, tail condition, expansion confirmation and release on a stable support
    Validated Electromagnetic Crane Approved ferromagnetic coils or other steel products under a verified lifting plan No mechanical insertion into the bore and potential remote engagement Steel grade, curvature, contact area, air gaps, scale or oil, temperature, banding, battery backup, retained-load strategy and proof testing
    Separate Maintenance Crane or Hoist Pumps, motors, rolls, covers and service lifts over the process section Keeps production coil crane duty separate and can target restricted maintenance areas Actual component weights, certified lifting points, access, acid exposure and interference with line equipment

    Architecture Selection

    Top-running double-girder cranes are commonly selected when coil mass, attachment weight, span, duty or positioning equipment requires higher structural capacity and accessible machinery arrangements. Single-girder solutions can suit lighter auxiliary service where duty, headroom and maintenance needs support that choice.

    A rotating hook block or powered attachment rotation may be required when coil eye orientation changes between transport, storage and line stations. The rotating envelope is verified against saddles, guards, columns and adjacent crane structures.

    rotating attachment crane platform considered for pickling line coil transfer
    Attachment rotation is specified only when the handling route requires a change in load orientation.

    Capacity, Duty and Performance Definition

    Gross Suspended Load

    The load calculation includes maximum coil mass plus the complete attachment, hook block, rotation mechanism, cables and any permanent equipment below the hoist. Capacity margin is not a substitute for a defined coil range or controlled attachment geometry.

    Operating Class and Load Spectrum

    Crane classification is selected from total working cycles, distribution of light and heavy loads, motion running time, starts per hour and expected service life. A crane that feeds every production coil normally requires a different fatigue evaluation from an occasional maintenance crane of the same rated capacity.

    Speeds and Cycle Time

    Main speeds are balanced against travel distance, line takt time, suspended-load stability and available deceleration zones. High top speed does not guarantee a shorter safe cycle. Controlled acceleration, anti-sway and accurate final approach often produce more repeatable throughput.

    Performance Data for the Specification

    • Maximum gross suspended load and complete coil range
    • Required hook or attachment travel and end approaches
    • Hoist, trolley and bridge main and creep speeds
    • Coils per hour and defined reference handling cycle
    • Placement tolerance at each automatic station
    • Availability target and planned maintenance allowance
    • Noise, power, braking and emergency operating criteria

    Coil Attachments for Pickling Lines

    The attachment controls engagement, load stability and coil contact. Its mass and center of gravity also affect crane capacity, headroom and wheel loads.

    C-Hook

    Suitable where the coil bore is accessible and the hook can enter without striking the saddle or line equipment. Throat depth, lower-arm section, counterweight, tip shape, lining and permissible coil range are engineered together.

    Powered Coil Tong

    Powered arms or jaws engage a defined coil range. Position feedback, load confirmation and fail-safe retention support assisted or automatic cycles, while moving parts require accessible inspection and corrosion protection.

    Inside-Diameter Lifter

    An expanding or positive-locking device engages the bore. ID tolerance, insertion depth, bore integrity, activation state and a mechanically secure lifting condition require verification for every coil family.

    Electromagnetic System

    Magnetic lifting is considered only after material, curvature, contact condition, air gap, surface oil or scale, temperature and retained-load behavior are validated. Ferromagnetic material alone does not establish a safe lifting capacity.

    Hook and Spreader Package

    A conventional hook, beam or maintenance attachment can support non-coil lifts. Changeover controls, dedicated stands, identification and proof-test records prevent an unapproved attachment from entering a production task.

    Surface Protection

    Replaceable pads, rounded contact edges and controlled contact pressure can reduce marking. Material compatibility, trapped contamination, inspection frequency and pad wear limits are specified.

    electromagnetic lifting platform illustrating a pickling line attachment option
    Henan Mine Crane publishes electromagnetic handling platforms; suitability for a specific pickled or oiled coil requires project-level validation.

    Acid-Mist and Corrosion-Control Design

    Corrosion protection is selected from the actual exposure map rather than a generic “acid-proof crane” label. Carbon-steel strip lines often use hydrochloric or sulfuric acid systems, while stainless and specialty lines can use different chemistries. Concentration, temperature and ventilation materially change the exposure.

    Design Area Required Input Possible Engineering Response
    Steel Structure Corrosivity, acid species, condensation, washdown and expected service life Prepared substrate, compatible coating system, sealed details where appropriate, drainage and defined inspection or repair intervals
    Electrical Equipment Mist, humidity, temperature, conductive deposits and cooling demand Selected enclosure and sealing, protected cable entries, conditioned or pressurized cabinets where justified, anti-condensation heating and corrosion-resistant terminals
    Mechanical Components Direct exposure, lubricant compatibility, service interval and cleaning method Protected brakes and bearings, compatible seals and lubricants, guarded rope path, replaceable wear parts and remote lubrication points
    Fasteners and Small Parts Galvanic compatibility, crevice exposure and maintenance practice Compatible materials and coatings, isolated dissimilar metals, accessible replacement and controlled tightening procedures
    Layout and Ventilation Mist plume, exhaust arrangement, prevailing air movement and cleaner zones Locate panels and service points away from concentrated mist, avoid liquid traps and coordinate crane route with fume capture equipment
    Separate protection concepts: corrosion resistance, enclosure ingress protection and explosion protection address different hazards. Explosion-protected equipment is selected only from the documented hazardous-area classification, gas or vapor group, temperature class and applicable local rules.
    steel mill crane structure requiring project-specific corrosion protection near a pickling line
    Protection is zoned by actual exposure so critical drives, brakes, sensors and electrical equipment remain inspectable and maintainable.

    Line Integration, Positioning and Automation

    Control scope can range from cabin or radio operation to assisted positioning and fully automatic coil transfer. Automation is defined by the process states, field interfaces and recovery strategy, not only by coordinate control.

    Station Handshakes

    The line PLC confirms station identity, coil availability, coil-car position, uncoiler or recoiler state, guards, gates and permission to enter. The crane returns approach, placement and task-complete states.

    Coil Identification

    Barcode, RFID, operator confirmation or production data links the physical coil with grade, order, dimensions, process status and destination. Exception rules prevent an unidentified coil from entering an automatic task.

    Position and Anti-Sway

    Absolute or referenced position data, controlled acceleration, sway reduction, load-height feedback and final approach logic support repeatable placement without using line equipment as a mechanical stop.

    Traffic and Protected Zones

    Crane-to-crane separation, vehicle lanes, restricted process areas, temporary maintenance zones and personnel access states are enforced through the agreed safety architecture.

    MES or WMS Interface

    Task messages define source, destination, coil identity and priority. Interface design also covers acknowledgements, duplicate commands, time synchronization, audit history, cybersecurity and network loss.

    Manual Recovery

    Every automatic sequence requires a controlled safe state and a documented recovery path for sensor failure, lost communications, incomplete engagement, blocked destination or interrupted power.

    automatic steel handling crane platform with positioning and plant data integration
    Henan Mine Crane publishes an automatic electromagnetic handling platform with positioning and MES integration; the pickling-line interface is engineered for the actual production system.

    Safety Functions and Operating Boundaries

    Overload and Motion Limits

    Rated-capacity protection, normal and final motion limits, brakes, buffers, travel warnings and monitored speed zones are selected under the governing code and risk assessment.

    Attachment Permissive

    Hoisting begins only after the approved engagement state is confirmed. Release is inhibited until the coil is supported, the destination is correct and the release sequence is authorized.

    Restricted-Area Control

    Barriers, gates, scanners, warning devices and administrative controls are coordinated around line entrances, vehicles, storage aisles and automatic crane operating zones.

    Collision Avoidance

    Adjacent cranes, building columns, line structures, high coils and temporary maintenance equipment are included in the collision model and stopping-distance calculation.

    Energy Isolation

    Lockout points, stored-energy release, access platforms and local isolation are coordinated for crane maintenance and work on interfacing line equipment.

    Abnormal Events

    The operating concept covers power loss, retained suspended load, failed attachment sensor, displaced coil, unavailable destination, fire alarm, ventilation loss and evacuation.

    steel processing crane installation requiring coordinated safety zones
    Safe operation depends on the complete load path, line state, personnel controls and verified attachment condition.

    Runway, Building and Maintainability Interfaces

    Existing Runway Verification

    Reuse requires verification of rail section and alignment, beams, brackets, columns, connections, foundations, fatigue history and measured condition. Maximum and minimum wheel reactions, lateral forces, buffer loads and electrification loads are issued for structural review.

    Clearance and Approach Study

    Hook approach, C-hook counterweight, tong arms, rotating envelope, cabin, walkways and festoon or conductor systems are checked in three dimensions against roof steel, ducts, exhaust equipment, lighting and the pickling line.

    Maintenance Access

    Inspection platforms, guarded access, safe parking position, component removal paths, lifting points, rope replacement space and isolation stations are defined before fabrication. Critical sensors and corrosion-prone parts remain visible and replaceable.

    Site Data Required

    • Building and runway drawings with verified dimensions
    • Rail elevation, span, length, end stops and expansion joints
    • Existing allowable vertical and horizontal reactions
    • Roof, duct, tank, line and vehicle clearances
    • Erection opening, laydown area and shutdown window
    • Electrical supply, grounding and communication network
    • Environmental survey and hazardous-area documentation

    Applicable Standards and Acceptance Testing

    The contract identifies the governing jurisdiction, crane design code, electrical standard and below-the-hook lifting-device rules. Common reference frameworks include ISO 4301, ISO 9927 and ISO 12480-1; EN 13001 and EN 15011; CMAA 70 and ASME B30.2; ASME BTH-1 and ASME B30.20 for applicable lifting devices; IEC 60204-32 for hoisting-machine electrical equipment; and ISO 13849-1 or IEC 62061 for safety-related control functions.

    ISO 12944 can inform protective-paint-system selection, while IEC 60529 addresses enclosure ingress ratings. IEC 60079, ATEX or IECEx requirements apply only where the project hazardous-area assessment establishes that scope. Local law and the approved contract remain controlling.

    Design Review

    Confirm load cases, classification, general arrangement, wheel loads, attachment envelope, corrosion schedule, electrical architecture, safety functions, interfaces and inspection access.

    Factory Acceptance Test

    Verify assemblies, controls, drives, braking, limits, sensors, attachment logic, alarms, interface simulation, documentation and agreed inspection records before shipment.

    Site Acceptance Test

    Test crane motions, load protection, representative coils, all transfer stations, placement tolerance, collision zones, line handshakes, abnormal states, manual recovery and operator procedures.

    Acceptance criterion: a successful proof load does not by itself validate production handling. Representative coil geometry, attachment engagement, process interfaces, cycle performance, corrosion-protection records and recovery behavior are tested against the approved specification.

    Published Adjacent Steel Mill References

    Published references demonstrate relevant steel-production crane and automation capabilities. They do not replace a project-specific pickling-line design review.

    Henan Mine Crane published Southeast Asia steel mill crane reference

    More Than 100 Lifting Units for a Southeast Asian Steel Mill

    Henan Mine Crane reports commissioning more than 100 lifting units for a large steel mill, including a 160 t double-girder overhead crane, slab clamping cranes, lower-rotating electromagnetic hanging-girder cranes and double-girder double-trolley gantry cranes.

    Evidence boundary: the published reference demonstrates multi-crane steel-mill delivery capability; it does not identify the units as pickling line cranes.

    View Published Reference →

    Henan Mine Crane automatic electromagnetic steel handling reference

    Automatic Electromagnetic Handling Platform

    Henan Mine Crane publishes an automatic electromagnetic hanging-girder solution with automatic operation, rigid-guide anti-sway, MES integration and multiple operating modes. These functions are relevant to automatic material-transfer architecture.

    Evidence boundary: the published solution is not presented as a pickling-line delivery, and magnetic suitability for a specific coil remains subject to load testing and risk assessment.

    View Automation Platform →

    Pickling Line Crane Price and Budget Scope

    A complete pickling line crane has no reliable catalog price because capacity, duty, attachment, corrosion protection, automation, runway interfaces and installation scope change the engineered package. Public prices reviewed on 21 September 2026 provide market context only and are not technically equivalent offers.

    Public Market Reference Published Price What the Figure Represents Major Exclusions or Limits
    10 t or 25 t C-Type Coil Lifting Hook Listing US$2,500–2,600 per set Marketplace attachment listing Not a crane; load range, material, lining, proof test, documentation, freight and project compliance require confirmation
    10 t Top-Running Double-Girder Crane Kit Listing US$33,020 Advertised crane kit with hoists Listing states “crane kit only”; excludes a pickling-line attachment, project corrosion package, runway, building work, installation and line automation
    Generic 60 t Double-Beam Bridge Crane Listing US$55,000–115,000 per set Marketplace complete-crane price signal No normalized pickling-line duty, coil attachment, acid-mist protection, automatic interfaces, civil works, erection or acceptance scope
    Complete Engineered Pickling Line Crane Project Project-specific RFQ Crane, attachment, controls and contracted project services A valid total requires an approved technical specification, site data, commercial boundary and destination

    Primary Price Drivers

    Capacity and span; operating class and speeds; C-hook, tong, mandrel or magnet; rotation; corrosion-control system; cabin and HVAC; positioning and anti-sway; automatic controls; safety zoning; line PLC and MES/WMS interfaces; runway electrification; documentation and local certification.

    Commercial Scope to Reconcile

    Runway rails and beams; structural strengthening; freight and insurance; taxes and duties; site supervision; mechanical and electrical installation; lifting equipment for erection; commissioning; load-test weights; training; spares; warranty support and production acceptance testing.

    Price interpretation: an attachment price, crane-kit price and installed automated project price describe different supply levels. Public listings may be promotional, provisional or equipment-only values. Comparable quotations require the same technical duty, exclusions, Incoterm, destination and acceptance obligations.

    Engineering and Procurement Deliverables

    A procurement-ready proposal defines performance, interfaces, evidence and commercial boundaries in measurable terms.

    Technical Proposal

    Design basis, general arrangement, main mechanisms, duty classification, speeds, attachment concept, protection package, control level and stated deviations.

    Interface Schedule

    Runway reactions, power and communications, line I/O, station coordinates, civil boundaries, erection needs, environmental inputs and third-party responsibilities.

    Safety Documentation

    Risk-assessment inputs, safety-function list, restricted zones, attachment logic, isolation concept, emergency states and required local conformity documents.

    Quality Records

    Material and welding records as specified, inspection and test plans, coating records, component certificates, attachment proof testing and factory test reports.

    Operation and Maintenance

    Manuals, lubrication plan, corrosion inspection, adjustment limits, fault recovery, spare-parts list, training scope and recommended preventive-maintenance intervals.

    Commercial Schedule

    Price, Incoterm, delivery milestones, packing, installation boundary, commissioning, training, acceptance, warranty, exclusions, validity and optional services.

    Pickling Line Crane RFQ Information

    The following data allows the crane, attachment, environmental protection, interfaces and project scope to be priced on a consistent basis.

    Coil and Attachment Data

    Material and grade; minimum and maximum mass, OD, ID and width; eye orientation; temperature; surface and oil condition; banding; center of gravity; contact restrictions; proposed C-hook, tong, ID lifter or magnet.

    Process and Duty Data

    Entry, exit, storage and dispatch sequence; station coordinates; lifts per hour; shifts; annual hours; load spectrum; travel distances; target cycle; availability target and required contingency.

    Environment and Site Data

    Acid chemistry, concentration and temperature; mist or corrosivity survey; humidity, condensation and washdown; ventilation; span, runway and clearances; power supply; building drawings and destination.

    Controls and Commercial Data

    Manual, assisted or automatic operation; placement tolerance; line PLC and MES/WMS protocols; safety zones; required code; Incoterm; freight, installation, commissioning, test and documentation boundaries.

    Frequently Asked Questions

    Where does a pickling line crane operate?

    Its principal production duties are usually in the incoming-coil, line-entry, line-exit, buffer, inspection and dispatch zones. It may also support planned maintenance, but the steel strip travels through the pickling tanks on the line equipment.

    Does every pickling line crane need acid-resistant construction?

    Protection depends on measured or specified exposure. Acid chemistry, mist, ventilation, humidity, condensation and washdown are mapped by zone. Coatings, enclosures, seals, materials and maintenance intervals are then selected for each zone.

    Is a C-hook or powered coil tong more suitable?

    A C-hook offers mechanical simplicity where the bore is accessible. A powered tong offers automated engagement and feedback for high-cycle service but adds mechanisms and maintenance. Coil geometry, cycle rate, access and control level determine the choice.

    Can an electromagnetic crane handle pickled coils?

    Only after the material grade, curved contact, air gaps, oil or moisture, banding, temperature, required holding force and power-loss behavior are validated. A mechanical attachment may be preferable where magnetic performance is uncertain.

    How is rated capacity determined?

    The starting value is the maximum gross suspended load: coil plus attachment, hook block and all equipment carried below the hoist. Operating class, dynamic effects, load distribution and governing code are then applied.

    How much does a pickling line crane cost?

    Public figures range from low-cost attachment or generic crane listings to substantially broader engineered projects. A defensible price requires coil data, span, duty, attachment, corrosion protection, automation, runway scope, destination and installation boundary.

    Can the crane connect to the line PLC and MES?

    Yes. The interface specification defines station states, task messages, coil identity, coordinates, acknowledgements, safety ownership, network protocol, cybersecurity, diagnostics and recovery after interrupted communications.

    Can an existing runway be reused?

    Only after its geometry, condition, fatigue history, rail alignment, beams, columns, connections and foundations are verified against the proposed vertical, lateral, longitudinal and buffer reactions.

    Request a Pickling Line Crane Quote

    Submit the coil range, handling sequence, line throughput, attachment preference, acid chemistry and exposure data, span, lift, runway information, control level, line-interface requirements, power supply, project destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.
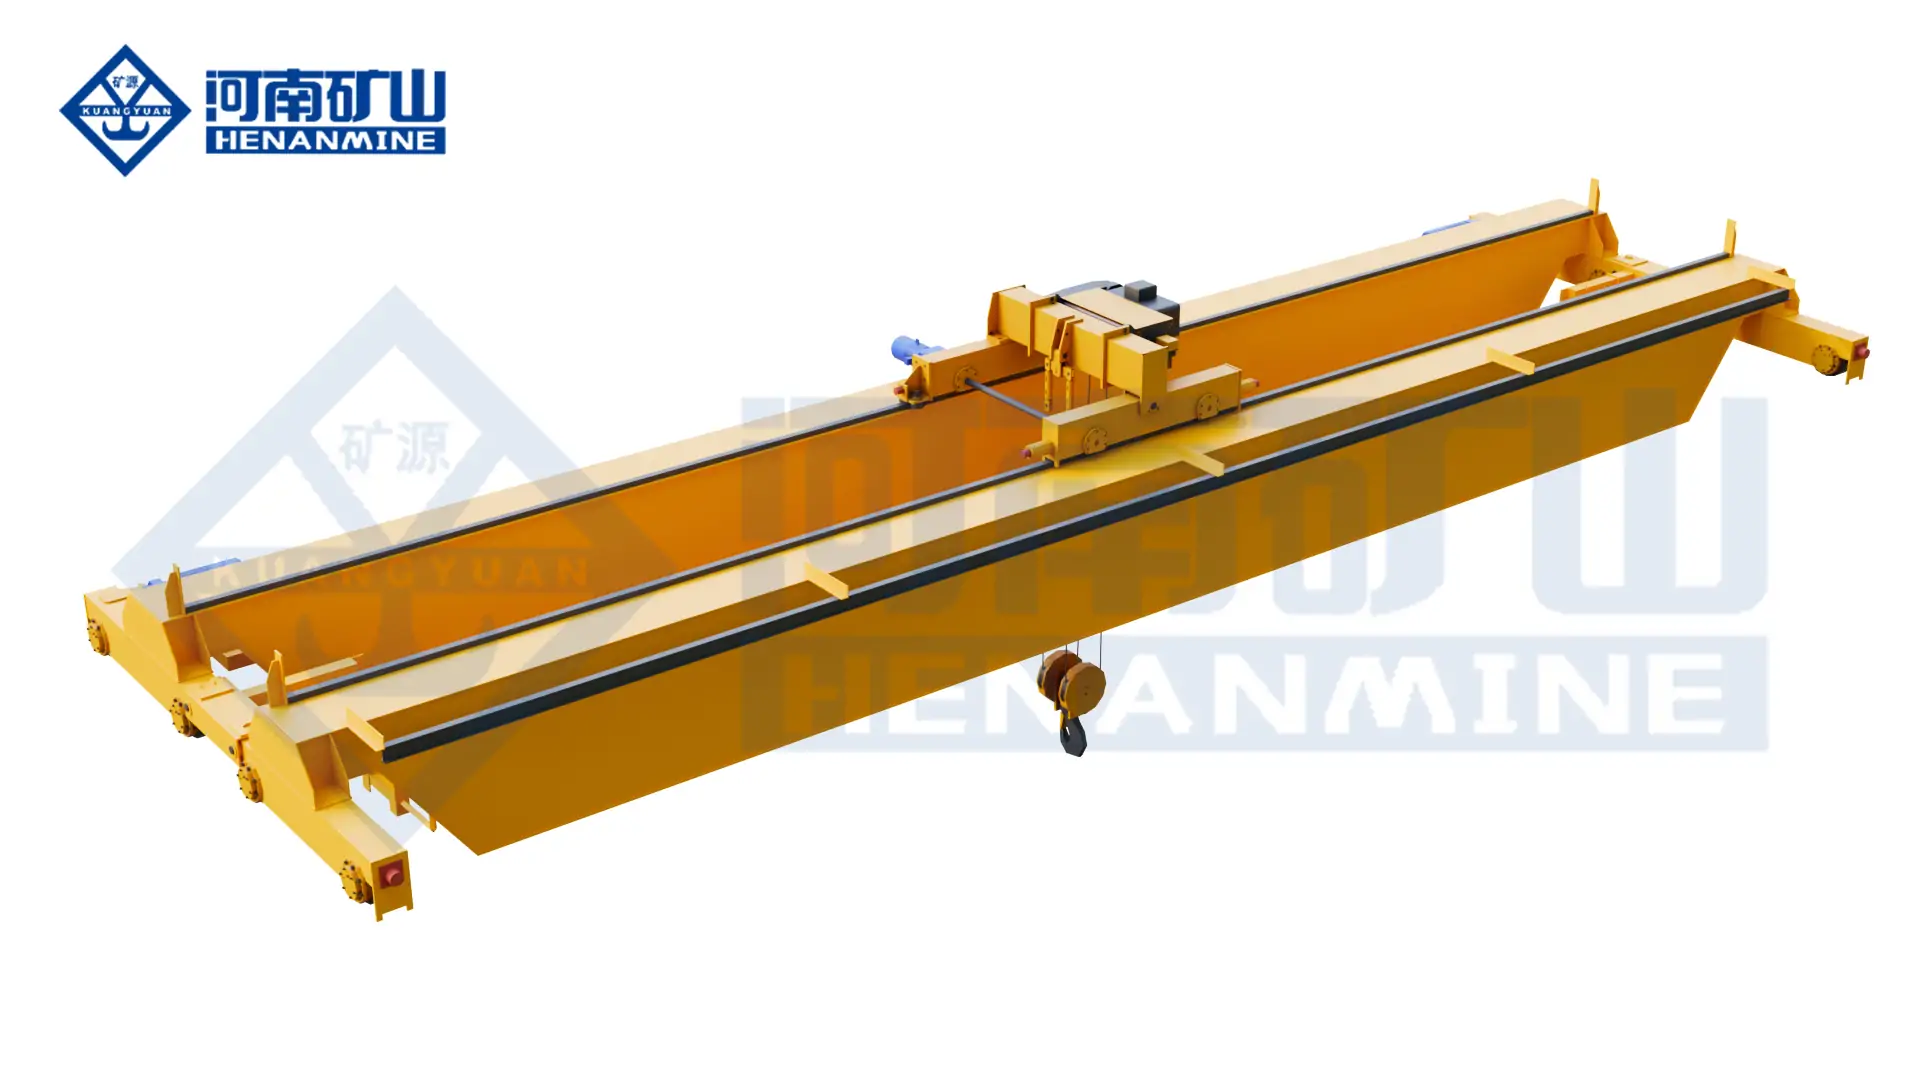
    Henan Mine CraneDiscuss your requirements ↗
  • Paper Mill Cranes

    Paper Mill Cranes

    Paper Mill Cranes

    Henan Mine Crane · Pulp and Paper Handling

    Paper Mill Cranes

    Overhead crane systems for paper-machine maintenance, reel and roll handling, converting operations and mill logistics. Henan Mine Crane configures the bridge structure, lifting mechanism, controls and load-handling attachment to the plant’s operating zone and duty schedule.

    Paper mills require different handling methods for machine components, paper rolls and raw materials. The proposed crane must match the actual load, handling frequency, building geometry and exposure conditions—not a generic industry label.

    overhead crane configuration shown for paper mill operations
    Crane selection starts with the paper mill’s material flow, lifting points and available building clearances.
    PRIMARY ZONESPaper Machine · Roll Store · Maintenance
    CRANE TYPESSingle · Double · Multi-Trolley
    LOAD HANDLINGHooks · Engineered Roll Attachments
    SUPPLY BASISProject-Specific Technical Offer

    Crane Systems Across a Paper Mill

    A paper mill crane may support machine installation and roll replacement, lift process equipment for maintenance, move parent rolls to converting lines or handle finished rolls in storage. A general-purpose hook crane can suit maintenance tasks, while dedicated reel handling may require a purpose-designed attachment and a more tightly controlled movement profile. Pulp bales, waste paper and loose bulk materials require separate gripping or grab arrangements.

    The mill layout determines whether these duties can be combined safely on one crane or require separate equipment. Henan Mine Crane offers bridge crane configurations for the defined process zones, including a three-trolley electric-hoist bridge crane described for paper-industry component handling and maintenance.

    Paper Mill Crane Selection Considerations

    The lifting schedule and plant interfaces determine the appropriate crane arrangement.

    01 · Load Definition

    Record heaviest reel, roll or machine component; include lifting beam, clamps, slings and other below-hook equipment in the required capacity.

    02 · Handling Geometry

    Confirm roll diameter, length, orientation, pickup and landing clearances, machine openings and permitted rotation.

    03 · Building Envelope

    Establish runway length, span, hook approach, available headroom, lifting height and existing column or runway loads.

    04 · Duty Profile

    Define lifts per hour, operating shifts, load distribution, travel distances and the time allowed for maintenance shutdowns.

    05 · Mill Environment

    Identify humidity, washdown, fibres and dust, corrosive chemicals, local temperature and any classified hazardous area.

    06 · Load Attachment

    Specify hooks, lifting beams, roll clamps or other approved attachments and the protection needed to prevent product damage.

    07 · Control and Access

    Choose pendant, radio or cabin control as appropriate; map operator visibility, access platforms and maintenance routes.

    08 · Plant Integration

    Coordinate crane operation with conveyors, production machines, pedestrian routes, fire protection and site electrical supply.

    Paper Mill Crane Configurations Compared

    The selection depends on the heaviest lift, the number of lifting points and whether the crane is assigned to maintenance or repeated process handling.

    Configuration Appropriate duty Important limitation
    Single-girder overhead crane Lighter maintenance and general material transfer Check hook height, span and actual duty before selection.
    Double-girder overhead crane Heavier machine components or demanding operating duty Confirm runway loads and the full building interface.
    Three-trolley bridge crane Separate lifting stations or engineered multi-point handling Coordinated lifting requires a defined load-sharing and control strategy.
    Dedicated roll-handling system Frequent parent-roll transfer and controlled placement Attachment compatibility and roll-damage prevention must be engineered separately.

    A three-trolley crane is not automatically a parent-roll handling system. Each lifting method and attachment must be qualified for its specified load and process.

    Technical Specification Schedule

    Item Basis for paper mill procurement
    Rated capacity Determine from the heaviest handling unit plus the lifting attachment; specify each trolley’s capacity separately where applicable.
    Span and lift Based on runway geometry, machine envelope, hook approach and clearances around rolls and equipment.
    Duty class Derived from actual load spectrum and cycles, not the paper-industry designation alone.
    Hoist and travel Speed and positioning response matched to throughput, product protection and maintenance lifts.
    Electrical protection Enclosure, cable routing and corrosion measures selected for measured humidity, dust and process exposure.
    Power and control Confirm site voltage, frequency, electrification, operator interface and any production-line interlock.

    As a product-specific example, the published three-trolley crane lists 1–32 t capacity, 7.5–31.5 m span, 6–30 m lifting height and A5–A6 working class. These figures describe that model’s published offering; they are not specifications for every paper mill crane or a commitment for a particular project.

    Handling Paper Rolls Without Compromising Product Quality

    A reel or parent roll is not a generic suspended load. The paper grade, roll diameter, core construction, wrap condition and acceptable contact pressure influence attachment selection. A hook crane can lift an approved beam or roll-handling device, but the attachment must be designed for the roll geometry and verified working load. Side clamps, core-engaging devices and vacuum systems have different operating envelopes and must not be treated as interchangeable.

    The operating procedure should define pickup orientation, load stability, allowable acceleration, transfer route and landing support. Drive settings and operator visibility should be reviewed alongside the lifting attachment to reduce swing and avoid contact with the paper machine, building or other stored rolls.

    Paper Mill Application Example: Three-Trolley Machine Maintenance

    Henan Mine Crane’s three-trolley electric-hoist bridge crane is presented for paper-industry component handling and equipment maintenance. Three independently positioned lifting stations can be specified where a machine component has multiple approved lifting points or where different workstations need access along one bridge.

    For a paper-machine maintenance lift, the engineering schedule identifies each component’s mass and centre of gravity, the lifting-point arrangement, trolley positions, combined bridge load, synchronized-motion requirement and path into the maintenance area. An approved lift plan and control philosophy govern any coordinated operation.

    Technical drawings, inspection records and applicable project references can be included in the vendor-qualification discussion.

    three trolley electric hoist bridge crane shown for paper industry component handling
    A multi-trolley arrangement requires engineered load sharing, lifting points and control coordination.

    Inspection, Installation and Lifecycle Support

    The supply specification should identify the applicable design standards, structural calculations, principal components, coating system and electrical enclosure requirements. The inspection plan should establish material traceability and the agreed fabrication, assembly, functional and load-testing checkpoints. Compliance documents are defined by contract and destination requirements; a generic certification statement cannot replace a project-specific compliance schedule.

    For an existing mill, runway suitability, column capacity, building access and shutdown windows must be assessed before production. Delivery planning should include erection space, rigging access, temporary power, isolation of nearby process equipment, testing and operator training.

    Maintenance planning covers hoists, brakes, wheels, travel drives, electrification and protective enclosures. Inspection frequency is determined by actual service, local regulations and the equipment manual. The spare-parts schedule should identify critical components against the mill’s acceptable downtime.

    Paper Mill Crane Price and Total Project Cost

    A paper mill crane price depends on capacity, span, duty, number of trolleys, lifting attachment, environmental protection, runway interface and the scope of site services. Public prices for general-purpose overhead cranes cannot be used as quotations for a three-trolley paper-machine crane or a dedicated roll-handling installation. The lifting attachment and mill integration may form a significant separate part of the investment.

    Crane Equipment

    Bridge, hoist or trolleys, drives, controls, electrification and specified protective equipment.

    Mill Interfaces

    Runway and building works, lifting attachment, production interlocks and equipment access changes.

    Delivery and Handover

    Packing, freight, installation, commissioning, inspections, training and initial spare parts.

    A comparable commercial offer identifies currency, Incoterm, technical inclusions, exclusions, commissioning responsibilities and warranty terms. Final price follows the confirmed mill layout and lifting schedule.

    Technical Information for Quotation

    Submit a mill layout and runway drawing; load list with dimensions, centres of gravity and approved lifting points; roll diameter, length, weight and handling orientation where applicable; travel and lift distances; operating cycles and shifts; humidity, dust and chemical exposure; electrical supply; required attachments; control and automation interfaces; destination; and the required delivery, installation and testing scope.

    Frequently Asked Questions

    What is a paper mill crane?

    An overhead lifting system configured for a specific pulp or paper production, maintenance or storage duty.

    Which crane handles paper-machine components?

    A properly rated hook crane or multi-trolley arrangement can be specified from the component mass, lifting points and maintenance route.

    Can the same crane handle parent rolls?

    Only with a qualified roll-handling attachment and a handling procedure matched to the roll and process.

    When is a three-trolley crane appropriate?

    Where multiple lifting stations or approved multi-point lifts justify separately controlled trolleys and engineered load sharing.

    Is an A5–A6 crane required in every paper mill?

    No. Working class follows actual operating cycles and load spectrum; A5–A6 describes the published three-trolley product range.

    How is rated capacity calculated?

    The heaviest permitted load includes the material and all below-hook lifting equipment, subject to the approved lift plan.

    What protection is needed for a humid mill?

    Electrical enclosure, cable and coating requirements are specified from actual moisture, washdown and chemical exposure.

    Can a crane be installed in an existing mill?

    Yes, subject to building and runway assessment, access for erection and a practical production shutdown plan.

    Is a roll-handling attachment included in the price?

    Only if included in the written equipment scope; roll clamps, beams or other devices should be itemized.

    What is needed for a firm quotation?

    Mill drawings, the load and lift schedule, environmental data, required attachments and the complete service scope.

    Related Overhead Crane Products

    Three-Trolley Electric-Hoist Crane

    Multiple lifting stations for engineered component handling.

    Double-Trolley Overhead Crane

    Two-point handling subject to coordinated-lift design.

    Single-Girder Overhead Cranes

    General mill service and selected lighter maintenance lifts.

    Double-Girder Overhead Cranes

    Higher-capacity machine-area and maintenance configurations.

    Overhead Crane Product Range

    Compare available overhead crane configurations.

    Paper Mill Lifting Proposal

    Request a Paper Mill Crane Quote

    Submit plant and runway drawings, the heaviest load and lift plan, roll specifications where relevant, operating cycles, environmental conditions, available power and project destination. Henan Mine Crane will prepare a defined equipment configuration and commercial scope.

    Henan Mine CraneDiscuss your requirements ↗
  • Overhead Travelling Crane

    Overhead Travelling Crane

    Overhead Travelling Crane

    Henan Mine Crane · Engineered Industrial Lifting Systems

    Overhead Travelling Crane

    Henan Mine Crane engineers overhead travelling cranes for workshop production, warehouse handling, machinery assembly, equipment maintenance, steel processing and project-specific lifting. Each system is configured around rated load, load spectrum, runway span, lifting height, operating frequency, building capacity, required speeds, control method and site environment.

    Also described as an overhead traveling crane, bridge crane or electric overhead travelling crane (EOT crane), the equipment provides powered hoisting, cross travel and long travel within a defined elevated runway area. Single-girder, double-girder, top-running and underhung arrangements are available for different building and production requirements.

    Henan Mine Crane electric overhead travelling crane in an industrial workshop
    Electric overhead travelling crane configured for full-bay lifting, cross travel and long travel. Final geometry and mechanisms follow the approved project design.
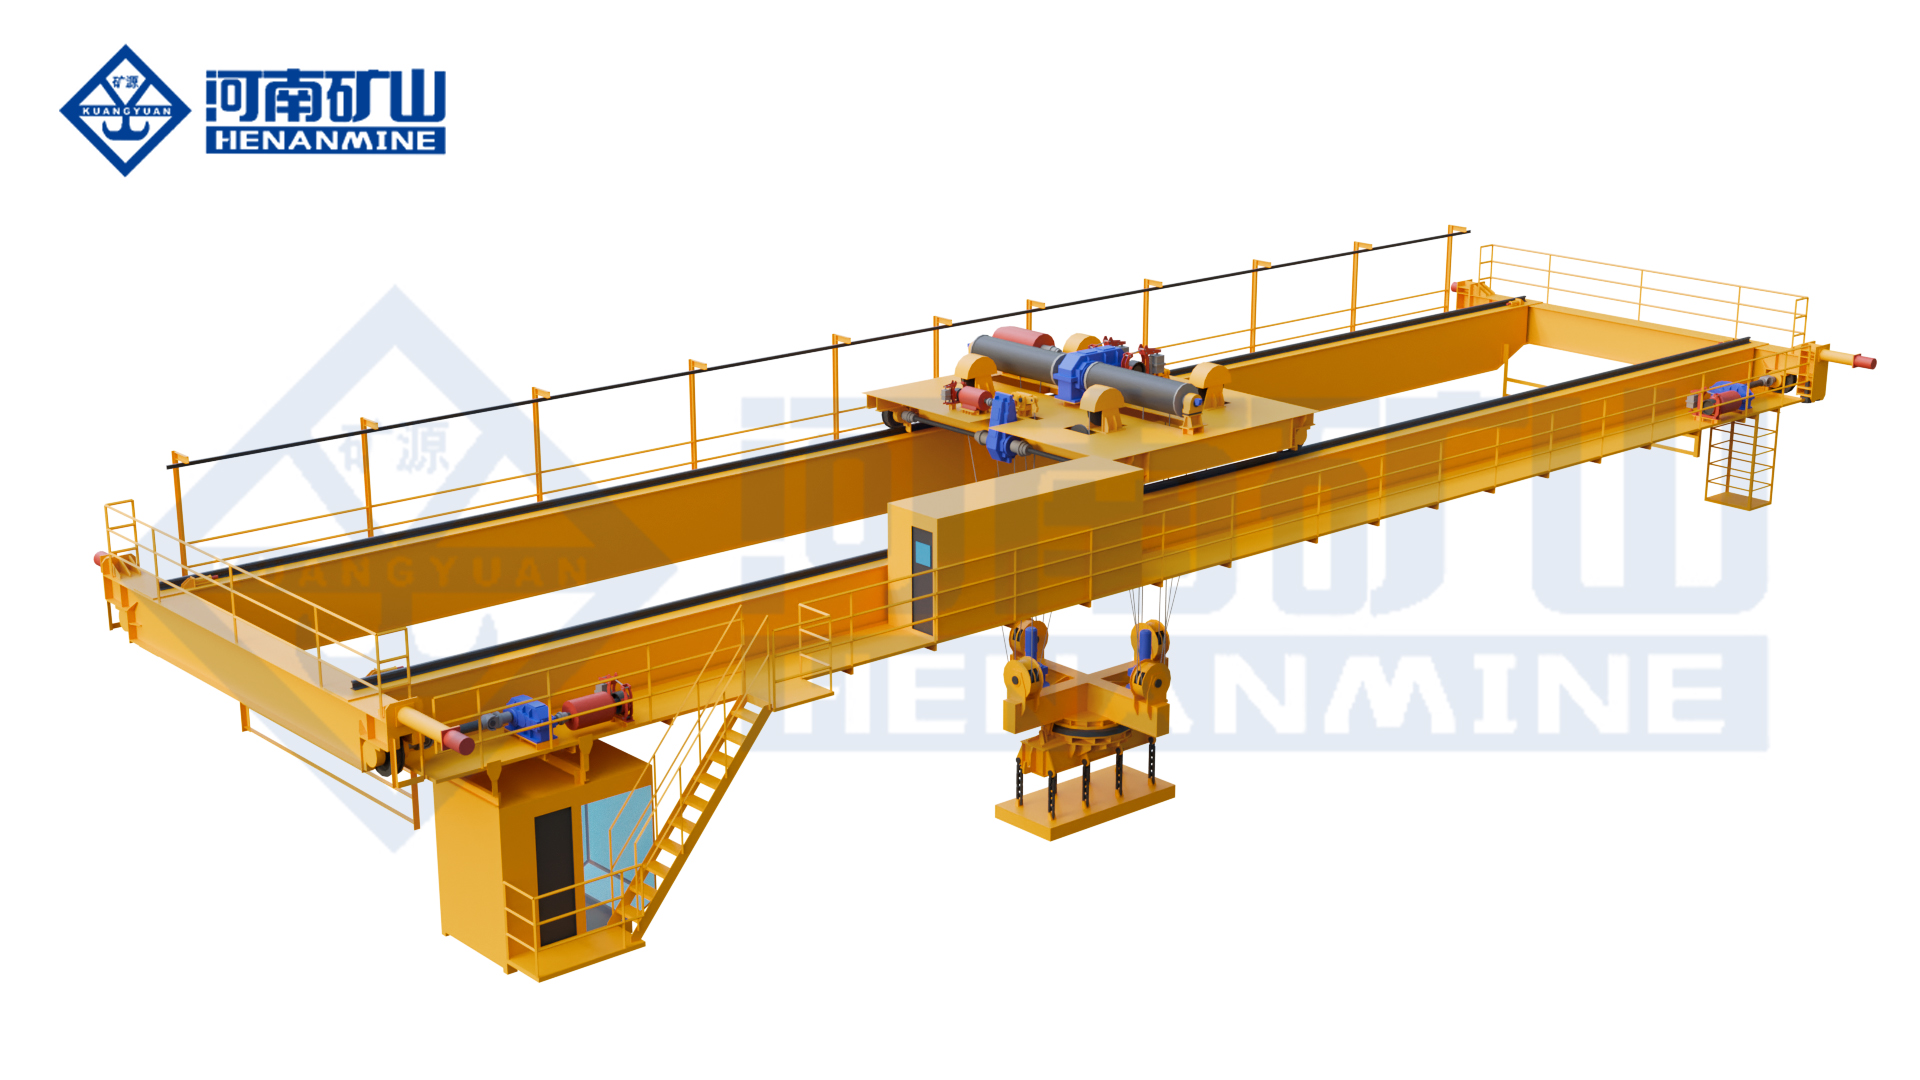
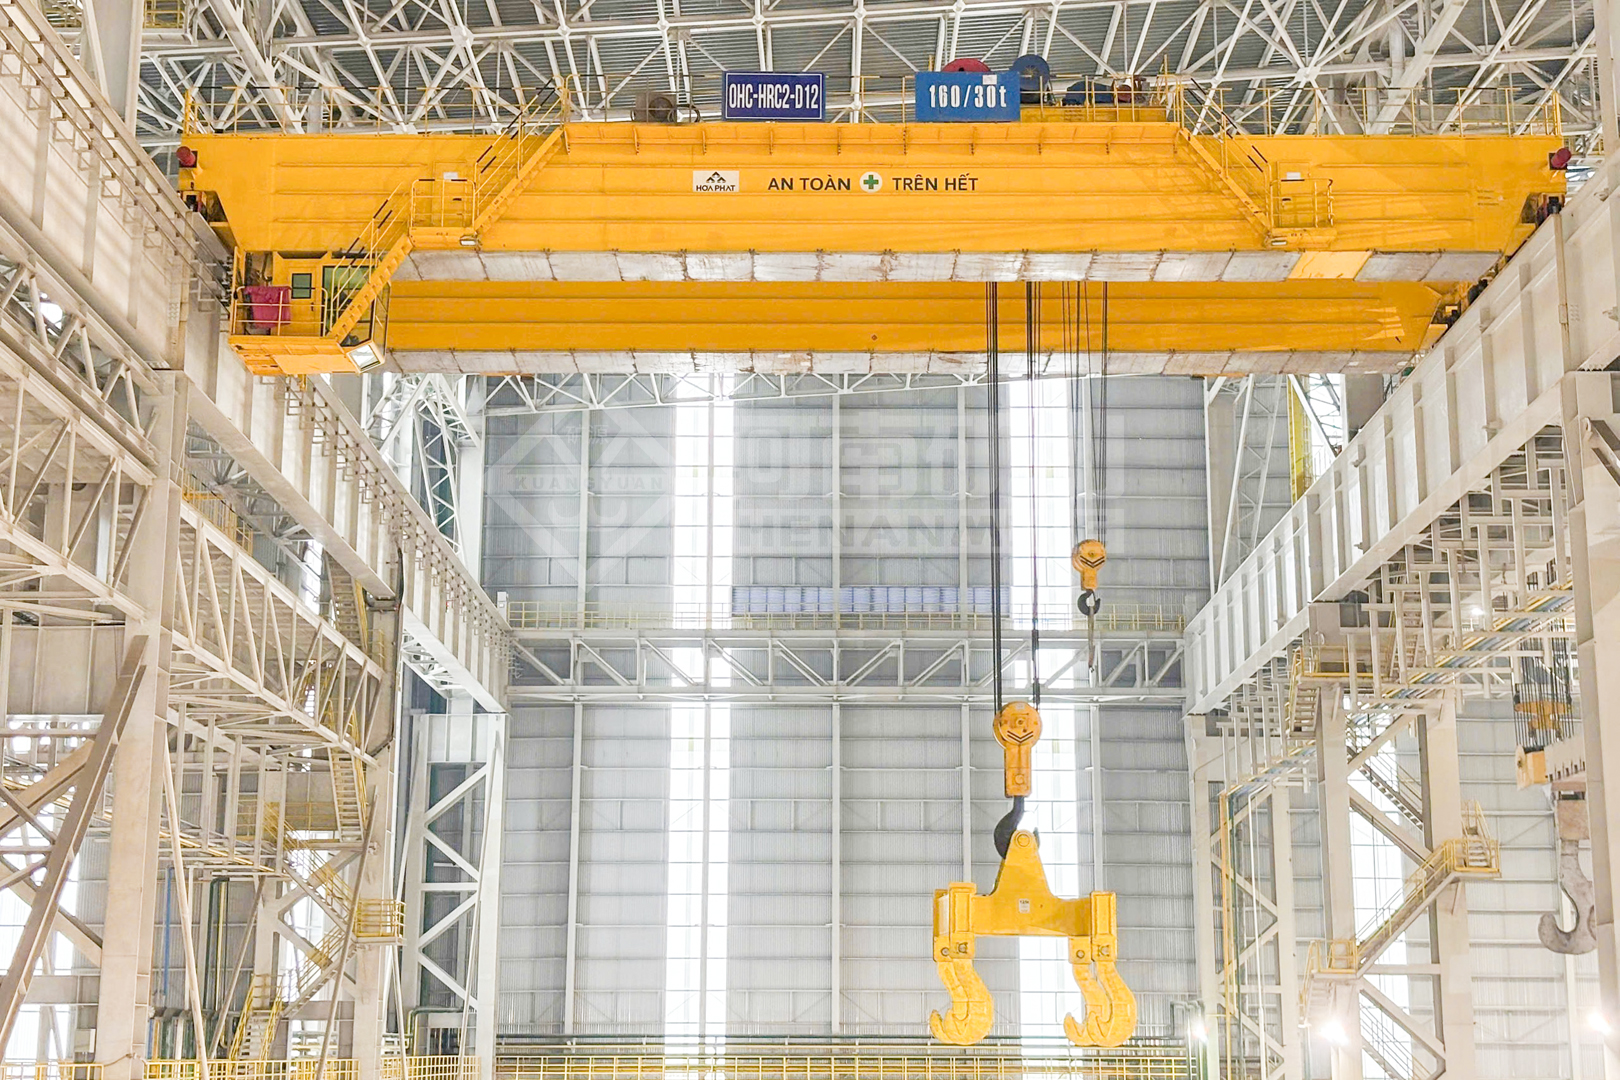
    BRIDGE ARRANGEMENT

    Single, Double or Underhung

    WORKING MOTIONS

    Hoist, Cross Travel, Long Travel

    CAPACITY AND SPAN

    Project-Engineered

    CONTROL OPTIONS

    Pendant, Radio, Cabin or Automatic

    What Is an Overhead Travelling Crane?

    An overhead travelling crane is a rail-guided lifting system with a bridge spanning the working bay. End carriages carry the bridge along elevated runway rails, while a hoist or trolley moves across the bridge. The hook therefore reaches a rectangular working area without permanent equipment occupying the production floor.

    The terms overhead travelling crane and overhead traveling crane differ only by British and American spelling. EOT crane emphasizes electrically powered operation. Bridge crane describes the structural arrangement. In normal industrial procurement, all three terms frequently refer to the same crane family, although the selected girder, trolley, runway and duty configuration can differ substantially.

    Production Handling

    Move raw material, workpieces, molds, fixtures and assemblies between production stations with defined hook coverage.

    Warehouse Transfer

    Support inbound handling, storage, order preparation and loading where floor traffic must remain clear.

    Assembly and Positioning

    Lift machinery, fabricated structures and large components with controlled travel speeds and optional precision positioning.

    Maintenance Lifting

    Provide planned access for motors, presses, turbines, machine tools and production-line equipment during maintenance work.

    Selection Considerations

    01 / LOAD

    Rated Load and Load Spectrum

    Define maximum and normal loads, attachment and rigging mass, load dimensions, centre of gravity and the percentage of lifts near rated capacity.

    02 / GEOMETRY

    Span, Lift and Approaches

    Establish runway gauge, required hook height, building clear height, end approach, side approach and obstructions above the operating area.

    03 / RUNWAY

    Building and Rail Capacity

    Review columns, brackets, runway beams, rail section, support spacing, alignment tolerances and permissible vertical and horizontal reactions.

    04 / DUTY

    Operating Cycle and Design Life

    State operating hours, starts and lifts per hour, travel distances, production criticality and expected service life under the selected classification system.

    05 / MOTION

    Speeds and Positioning

    Set hoisting, trolley and bridge speeds from cycle-time and positioning requirements. Variable-frequency control supports smooth acceleration and deceleration.

    06 / ENVIRONMENT

    Temperature and Protection

    Identify indoor or outdoor service, dust, humidity, corrosion, radiant heat, hazardous media and cleanliness requirements before equipment selection.

    07 / CONTROL

    Operator and Process Interface

    Select pendant, radio remote, cabin or automatic operation and define anti-sway, positioning, interlocking and production-line communication needs.

    08 / PROJECT

    Standards and Supply Boundary

    Confirm destination regulations, governing design standard, power supply, inspection plan, documentation language, freight term and installation responsibilities.

    Rated capacity alone is insufficient for crane selection. A 10 t maintenance crane used a few times per week and a 10 t production crane making repeated near-capacity lifts require different mechanism classes, controls, brakes, wheel loads and lifecycle provisions.

    Compare Overhead Travelling Crane Configurations

    The preferred configuration depends on the relationship between the load, bridge span, headroom, runway position, building reactions and operating intensity. The table establishes an initial engineering direction; final selection requires project data.

    Configuration Principal Advantage Typical Application Critical Design Input
    Single-Girder Top-Running Lower bridge mass and compact electric-hoist arrangement General workshop, warehouse, assembly and maintenance Building reactions, headroom, span and required duty
    Double-Girder Top-Running Greater structural and trolley configuration flexibility Heavier loads, wider spans and demanding production duty Load spectrum, wheel loads, trolley type and hook approach
    Underhung Travelling Crane Suspended runway preserves floor area and supports flexible layouts Space-restricted plants, hangars and selected large-span facilities Roof capacity, suspension points, runway geometry and clearances
    Freestanding Bridge System Independent columns avoid relying on the existing building structure Retrofit projects or buildings without suitable crane runway supports Foundation capacity, column locations and floor-level interfaces
    Gantry Crane Leg-supported bridge operates without elevated building runways Outdoor yards, construction, fabrication and temporary assembly areas Ground rails, foundations, wind, legs and outdoor protection

    Hoisting, Cross Travel and Long Travel

    double girder overhead travelling crane showing bridge and trolley motion
    Double-girder bridge arrangement with powered hoisting, trolley cross travel and bridge long travel along the runway.

    Vertical Hoisting Motion

    A wire-rope electric hoist, electric chain hoist or open-winch trolley raises and lowers the load. Capacity, lifting height, reeving, motor duty, brake arrangement and required creep speed determine the hoisting mechanism.

    Trolley Cross Travel

    The hoist or trolley moves across the bridge to position the hook across the bay. Side approach, trolley wheelbase, rail arrangement and service access affect usable coverage.

    Bridge Long Travel

    End carriages move the complete bridge along parallel runway rails. Wheel loads, drive coordination, rail alignment, skew behavior, buffers and end limits require review as one travel system.

    Smooth Motion and Positioning

    Single-speed operation can suit simple maintenance tasks. Dual-speed or variable-frequency control improves acceleration, deceleration and final positioning. Anti-sway and automatic positioning are available where production flow justifies the additional control scope.

    Overhead Travelling Crane Specifications

    Overhead travelling cranes are project-configured rather than selected from capacity alone. The following schedule identifies the principal parameters that must appear in a technical proposal and purchase specification.

    Parameter Available Engineering Direction Required Project Definition
    Rated capacity Light, medium, heavy and project-specific lifting capacities Payload, attachment mass, dynamic effects and required safety allowance
    Bridge structure Single girder, double girder, top-running or underhung Span, headroom, hook approaches, building loads and maintenance access
    Hoisting mechanism Chain hoist, wire-rope hoist, open-winch trolley or special mechanism Capacity, lift, reeving, duty, speed, redundancy and load type
    Span and lifting height Custom to runway gauge and operating envelope Measured building section, rail elevation, floor level and highest load position
    Working class Selected under the specified ISO, FEM, CMAA or local classification basis Operating time, starts, load spectrum, cycles and production criticality
    Motion speeds Single speed, dual speed or variable-frequency control Required cycle time, load stability, approach speed and positioning tolerance
    Operator control Pendant, radio remote, cabin, remote station or automatic system Visibility, travel distance, staffing, process interface and risk assessment
    Power supply Three-phase supply and control voltage matched to the destination site Voltage, frequency, earthing system, feeder position and available fault level
    Load attachment Hook, lifting beam, grab, magnet, clamp or custom below-hook device Load shape, temperature, pickup method, attachment mass and loss-of-power response
    Environmental protection Dust, corrosion, high-temperature, explosion-protected or clean configuration Ambient data, hazardous-area classification, contaminants and enclosure requirements

    Frequently requested capacity groups include 1–5 t, 5–20 t, 20–50 t and 50 t+. These groups are procurement starting points rather than fixed model limits. Span, duty, building reactions and process risk can change the preferred crane structure within the same capacity.

    Building, Runway and Electrical Interfaces

    Runway Survey and Structural Review

    Existing runway beams and supporting structures require verified dimensions, rail condition, alignment, elevation, support spacing and allowable reactions. New buildings require early coordination of crane wheel loads and horizontal forces with the structural designer.

    Headroom and Hook Coverage

    Rail elevation, roof bracing, lights, ducts, sprinklers and adjacent equipment can restrict crane depth and hook travel. End and side approaches should be shown on the approved general arrangement rather than assumed from nominal span.

    Power Distribution

    The supply scope can include runway conductor bars or festoon systems, bridge cross-travel electrification, isolation, control transformer, protective devices and earthing. Interface positions and incoming cable responsibilities belong in the commercial schedule.

    Multiple-Crane Operation

    Shared runways may require anti-collision devices, working-zone limits and coordinated maintenance isolation. Tandem lifting requires a separately engineered control and load-sharing arrangement.

    underhung overhead travelling crane and suspended runway in a large workshop
    Suspended runway layout demonstrating the importance of support positions, roof capacity, clearances and runway geometry in overhead crane selection.

    Controls, Safety Functions and Load Handling

    Hoisting Protection

    Overload limitation, upper and lower limits, brakes, rope guidance, hook latches and project-specific overspeed or redundancy functions protect the lifting motion.

    Travel Protection

    Bridge and trolley travel can include end limits, buffers, emergency stops, motor protection, braking supervision and anti-collision devices for shared runways.

    Controlled Positioning

    Variable-frequency drives, low-speed approach, anti-sway, encoders and selected positioning functions support stable load movement and repeatable process handling.

    Special Attachments

    Lifting beams, magnets, grabs, clamps and purpose-built attachments require defined load cases, interlocks, power-loss response and inspection provisions.

    The final safety architecture follows the risk assessment, selected crane standard, destination regulations, working environment and handled material. Component names alone do not establish compliance; functions, setpoints, test methods and documentation must be defined in the technical agreement.

    Representative Overhead Travelling Crane Projects

    Project requirements range from one large-capacity crane for precision component installation to coordinated crane fleets serving several production lines. The following cases demonstrate both engineering conditions.

    300 ton double girder overhead travelling crane for bridge construction
    Large-capacity double-girder overhead travelling crane developed for heavy component lifting and installation in a major bridge-construction project.

    PROJECT CASE 01 · HEAVY ENGINEERING

    300 t Double-Girder Overhead Travelling Crane

    CAPACITY

    300 t

    STRUCTURE

    Double Girder

    APPLICATION

    Bridge Construction

    Henan Mine Crane developed the crane as core lifting equipment for the Zhangjinggao Yangtze River Bridge project. The modular double-girder arrangement addresses large component handling, installation access and transport segmentation.

    The project configuration includes full variable-frequency motion control, hardened-gear drive components and integrated electrical design. This case demonstrates the engineering depth required when capacity, precision, long operating periods and project logistics must be resolved together.

    Review the 300 t Crane Project

    industrial overhead crane fleet for a high-capacity manufacturing plant
    Coordinated industrial crane package for high-volume production, material transfer and production-line equipment handling.

    PROJECT CASE 02 · MULTI-CRANE PRODUCTION FACILITY

    150-Crane Package for a 6-Million-Ton Industrial Plant

    PACKAGE

    Up to 150 Cranes

    LISTED CAPACITIES

    100 t and 125+125 t

    PLANT CAPACITY

    6 Million t/year

    This industrial project required a batch crane package across material handling, equipment assembly and production processes. Individual crane specifications were assigned to different workstations instead of applying one standard configuration throughout the plant.

    The disclosed equipment family includes 100 t intelligent cranes and 125+125 t cranes with variable-frequency control, position tracking, production-line interfaces, monitoring and redundant safety provisions. The case demonstrates multi-model engineering and coordinated delivery for a continuous-production facility.

    Review the Industrial Crane Package

    Comparable Project Scope

    A technically comparable crane case should identify capacity, span, lifting height, working class, load spectrum, mechanism arrangement, control philosophy, runway interface, environment and delivery boundary. Matching capacity without matching operating conditions does not establish an equivalent crane.

    Engineering, Manufacturing and Project Documentation

    A reliable purchase specification defines the design basis, manufacturing controls, inspection points and handover records before production begins. Henan Mine Crane can align the project document schedule with the destination requirements and agreed supply scope.

    Engineering Package

    • Design criteria and classification basis
    • General arrangement and hook-coverage drawing
    • Wheel loads and runway interface data
    • Electrical architecture and control narrative

    Manufacturing Controls

    • Material identification and inspection scope
    • Welding, dimensional and structural checks
    • Wheel, end-carriage and mechanism alignment
    • Surface preparation and coating inspection

    Testing and Handover

    • Factory functional and control checks
    • Inspection records and component certificates
    • Site commissioning and agreed load testing
    • Operation, maintenance and spare-parts documents

    Required standards, third-party inspection, witness points, certificate formats and document language should be listed in the inquiry. Certification must be confirmed for the selected crane and destination rather than inferred from a different product or project.

    Delivery, Installation, Commissioning and Maintenance

    Shipment and Site Readiness

    Transport segmentation, packing, unloading access, erection equipment, runway completion, electrical supply and working permits should be confirmed before dispatch.

    Erection and Alignment

    Installation covers bridge assembly, end-carriage alignment, hoist or trolley installation, electrification, rail interface checks and verification of required clearances.

    Commissioning and Acceptance

    Commissioning verifies mechanisms, brakes, limits, controls, alarms, travel behavior and agreed load tests. Acceptance responsibilities follow the project contract and local regulations.

    Lifecycle Maintenance

    Routine inspection covers ropes or chains, hooks, brakes, wheels, rails, fasteners, lubrication, electrical devices and safety functions. Intervals follow duty, environment and applicable requirements.

    Overhead Travelling Crane Price and Cost Scope

    Current international equipment listings for basic new overhead travelling cranes commonly begin at approximately US$3,000–US$9,000. A practical early equipment budget for standard industrial single- or double-girder systems is approximately US$8,000–US$100,000+, depending on capacity, span, lifting height, working class, hoist or trolley design and control scope.

    These figures are preliminary market-planning ranges, not fixed Henan Mine Crane selling prices. Heavy-duty, explosion-protected, metallurgical, automated or unusually wide-span cranes require an engineered quotation. A complete installed-system budget may be substantially higher when runway structures, building reinforcement, freight, erection, commissioning and local inspection are included.

    Cost Package Typical Inclusions Principal Cost Drivers
    Crane Equipment Bridge, end carriages, hoist or trolley, controls and specified safety functions Capacity, span, lift, duty, speeds, environment and attachment
    Runway and Power Rails, runway beams, columns, conductor system, isolators and incoming feeder interfaces Runway length, building capacity, foundation scope and local electrical design
    Logistics Packing, inland transport, ocean freight, insurance and destination handling as agreed Shipment dimensions, delivery term, destination and route restrictions
    Site Services Survey, erection supervision, installation, commissioning, load test and training Site access, labor, erection equipment, test loads and regulatory inspection

    A valid price comparison uses the same capacity, span, lifting height, working class, speeds, protection, control scope, runway boundary, documentation, delivery term and site-service responsibilities. A crane equipment price cannot be compared directly with a complete installed-system price.

    Overhead Travelling Crane FAQ

    Is an overhead travelling crane the same as an EOT or bridge crane?

    The terms commonly describe the same crane family: a bridge travels along elevated runways and a hoist or trolley moves across the bridge. EOT emphasizes electric operation, while bridge crane emphasizes the supporting structure.

    What is the difference between travelling and traveling crane?

    Travelling is standard British spelling and traveling is standard American spelling. The equipment and operating principle are the same.

    Should a single-girder or double-girder crane be selected?

    Single-girder cranes suit many general industrial applications where lower bridge mass and compact electric-hoist construction satisfy the load and duty. Double-girder cranes provide additional rigidity and configuration space for heavier loads, wider spans, demanding duty or improved hook approaches.

    Can an overhead travelling crane be installed in an existing building?

    Installation may be possible after verifying runway beams, columns, brackets, roof clearances, rail alignment, electrical supply and erection access. A freestanding runway can be evaluated where the building cannot support crane reactions.

    How is the required duty class determined?

    Duty classification considers total operating time, starts per hour, load spectrum, travel distances, lifting cycles and production criticality under the specified standard. Rated capacity alone does not determine duty.

    Which control method is suitable?

    Pendant control supports local operation. Radio remote control provides flexible viewing positions. Cabin control suits long travel, intensive duty or visibility-critical work. Automatic control is evaluated for repetitive production and system integration.

    How much does an overhead travelling crane cost?

    Basic new equipment listings commonly begin around US$3,000–US$9,000. Standard industrial single- or double-girder equipment often requires an early budget of approximately US$8,000–US$100,000+. Runways, freight, installation and local inspection can add substantial cost.

    Are runway beams and rails included in the crane quotation?

    Only when expressly included. The commercial schedule should identify crane equipment, rails, runway beams, columns, conductor system, building work, freight, installation, commissioning and testing as separate scope items.

    Can variable-frequency control and anti-sway be supplied?

    Variable-frequency control can be configured for hoisting, trolley and bridge travel. Anti-sway, positioning and process interlocks can be integrated where the handling cycle, load behavior and required accuracy justify the control functions.

    What information is required for a quotation?

    The RFQ should include rated and normal loads, span, lifting height, runway length, building section, operating cycles, required speeds, control method, environment, power supply, project country, applicable standards and delivery and installation scope.

    Request an Overhead Travelling Crane Quote

    Henan Mine Crane prepares a project-specific configuration and commercial scope from the operating requirement and site data. The RFQ should include:

    • Maximum and normal loads, load dimensions, attachment and lifting method.
    • Runway span, lifting height, runway length, rail elevation and building section.
    • Operating hours, lifts per hour, load spectrum and required motion speeds.
    • Control method, positioning requirement and production-line interface.
    • Temperature, dust, corrosion, hazardous media and indoor or outdoor conditions.
    • Power supply, project country, required standards, inspection plan and installation boundary.
    Henan Mine CraneDiscuss your requirements ↗