Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

博客

  • Coil Handling Crane Systems

    Coil Handling Crane Systems

    Coil Handling Crane Systems

    Henan Mine Crane · Engineered Coil Transfer and Storage Systems

    Coil Handling Crane Systems

    Overhead cranes engineered for steel and aluminum coil receiving, process-line feeding, storage, retrieval, truck or rail loading and automated warehouse logistics.

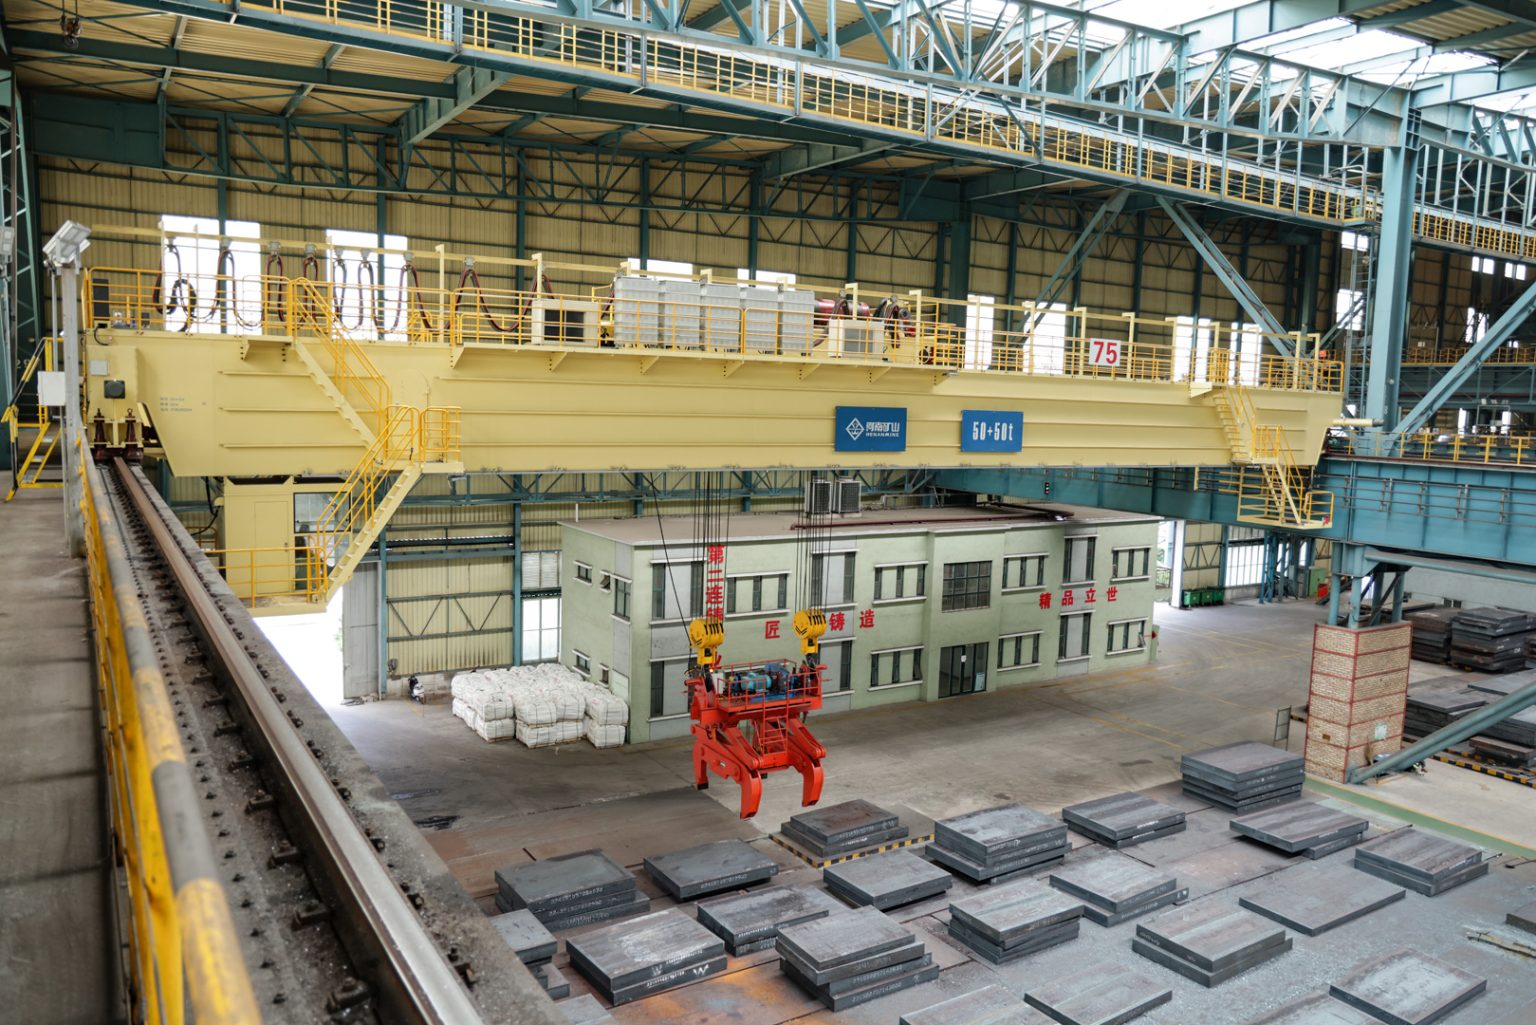
    Henan Mine Crane configures each coil handling crane around the maximum gross suspended load, coil outside and inside diameters, width, eye orientation, attachment, surface-protection requirement, cycle rate, runway interface and control level. Available project concepts include hook cranes with C-hooks, motorized coil tongs, inside-diameter lifters, validated magnetic systems and coordinated automatic warehouse cranes.

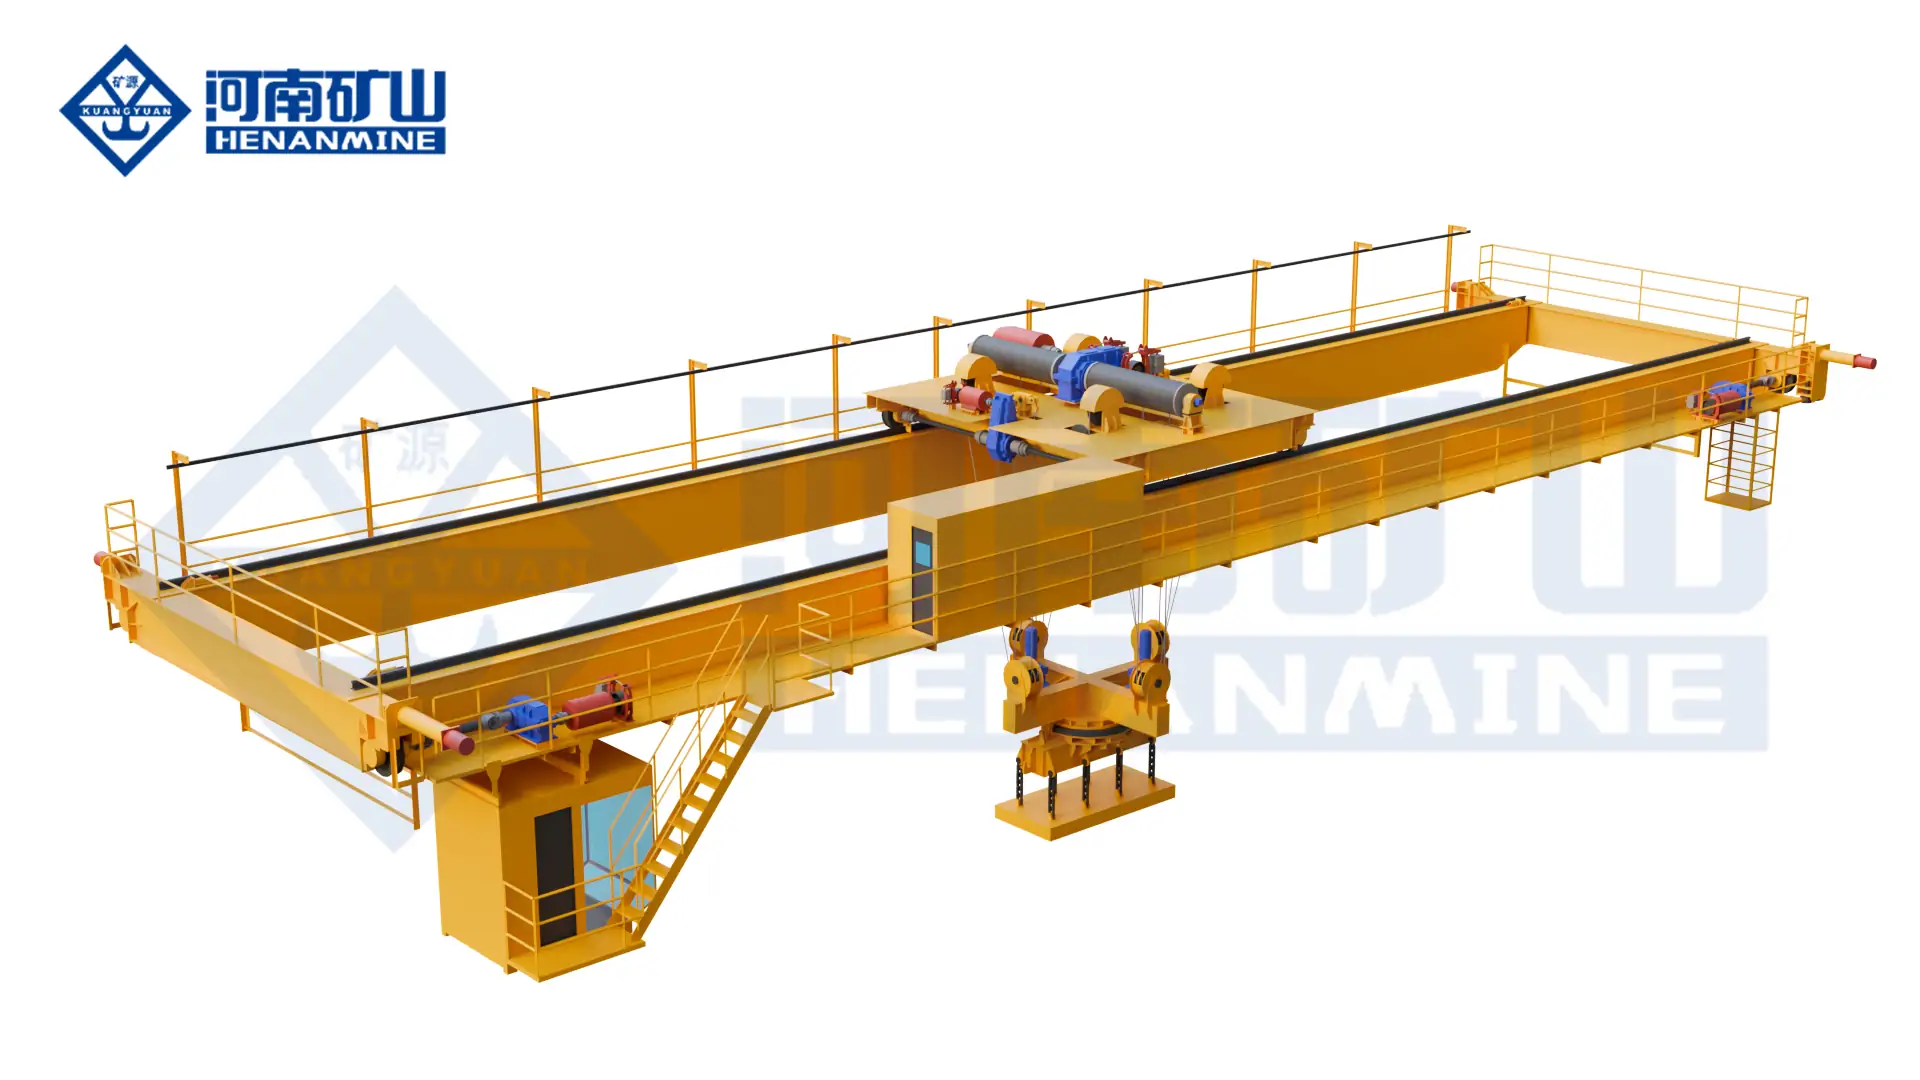
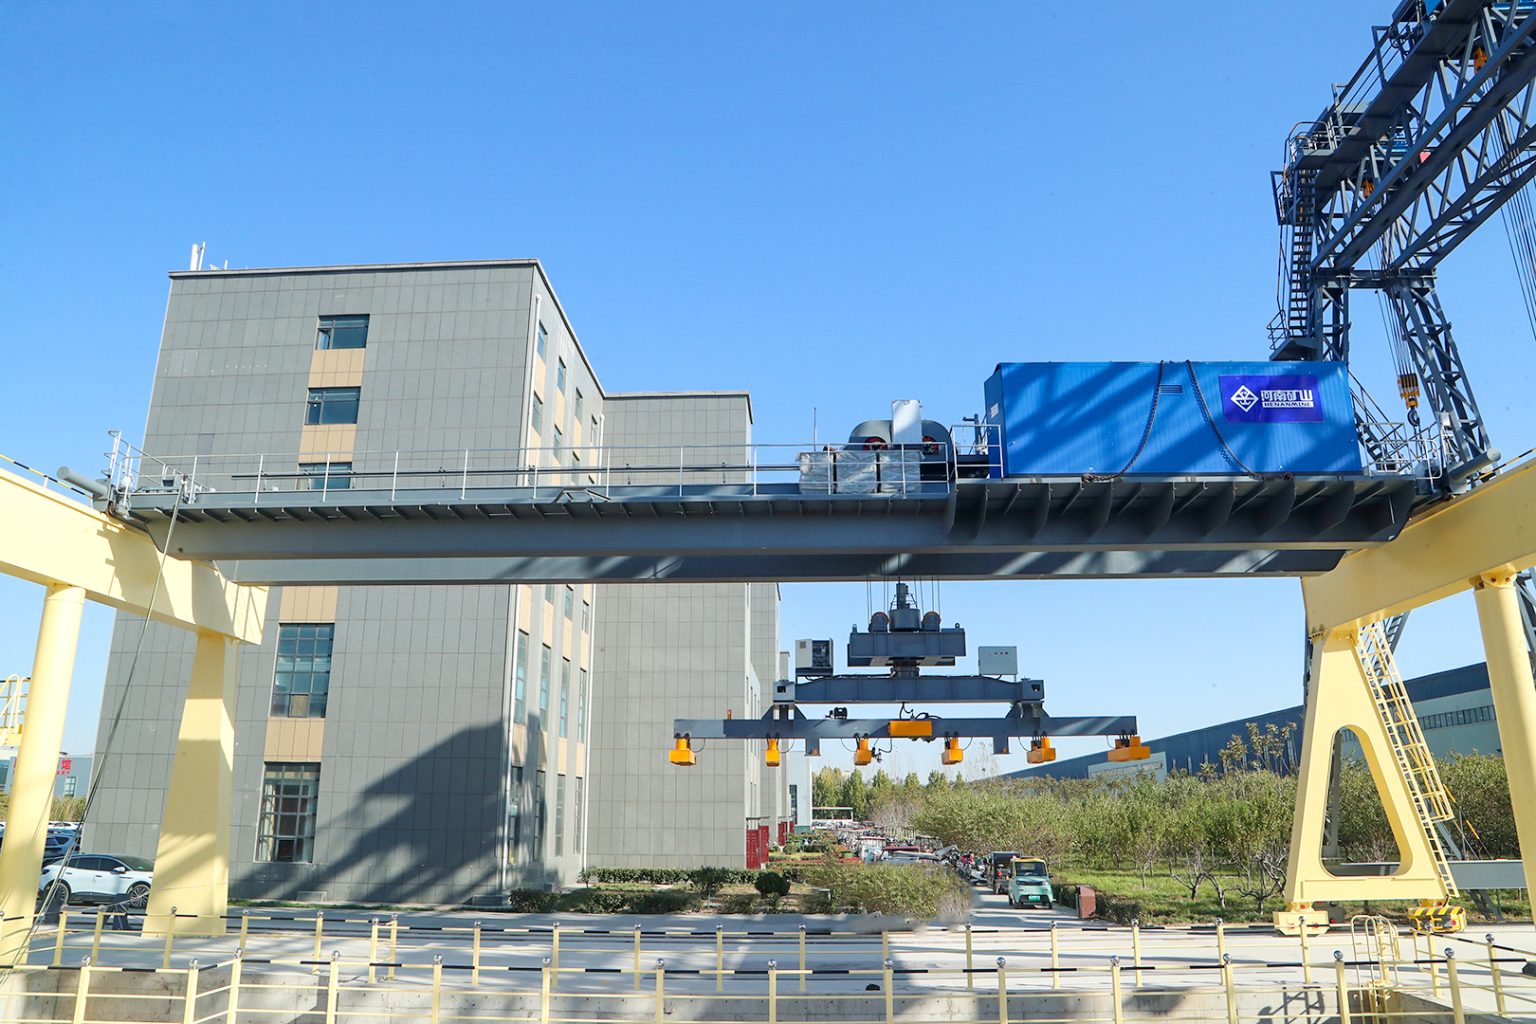
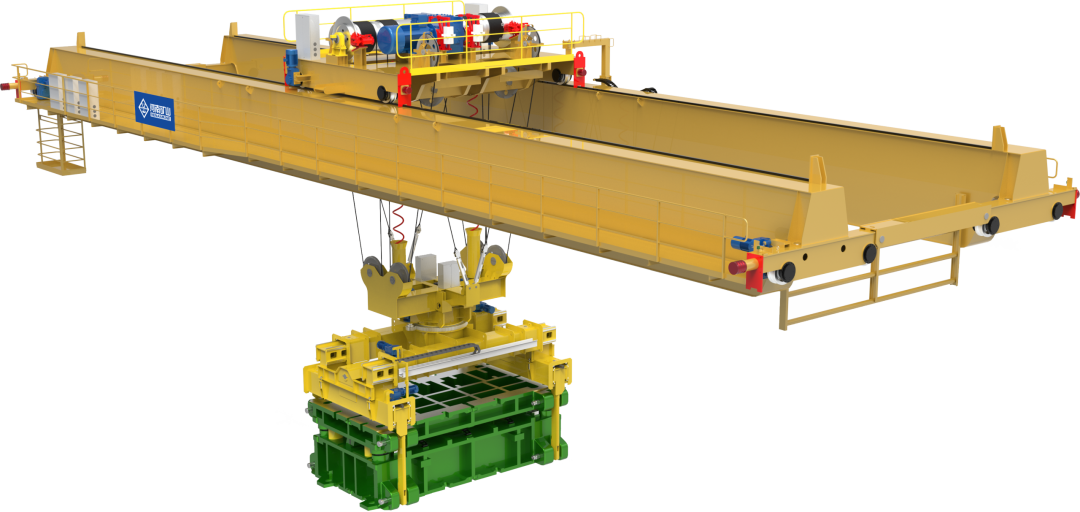
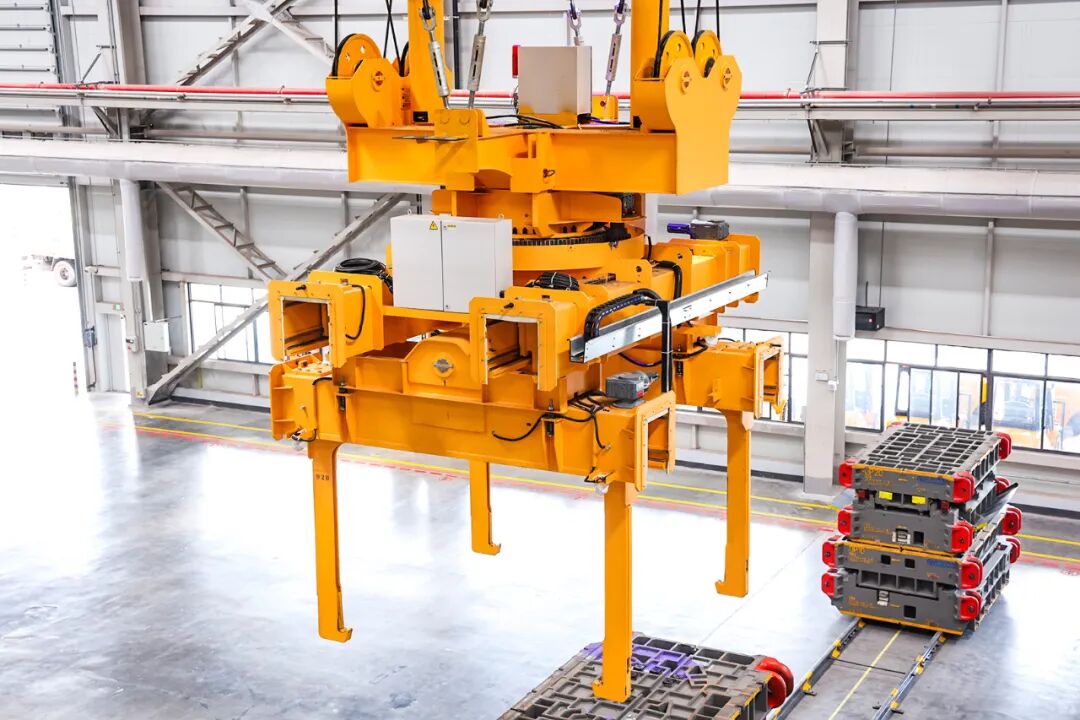
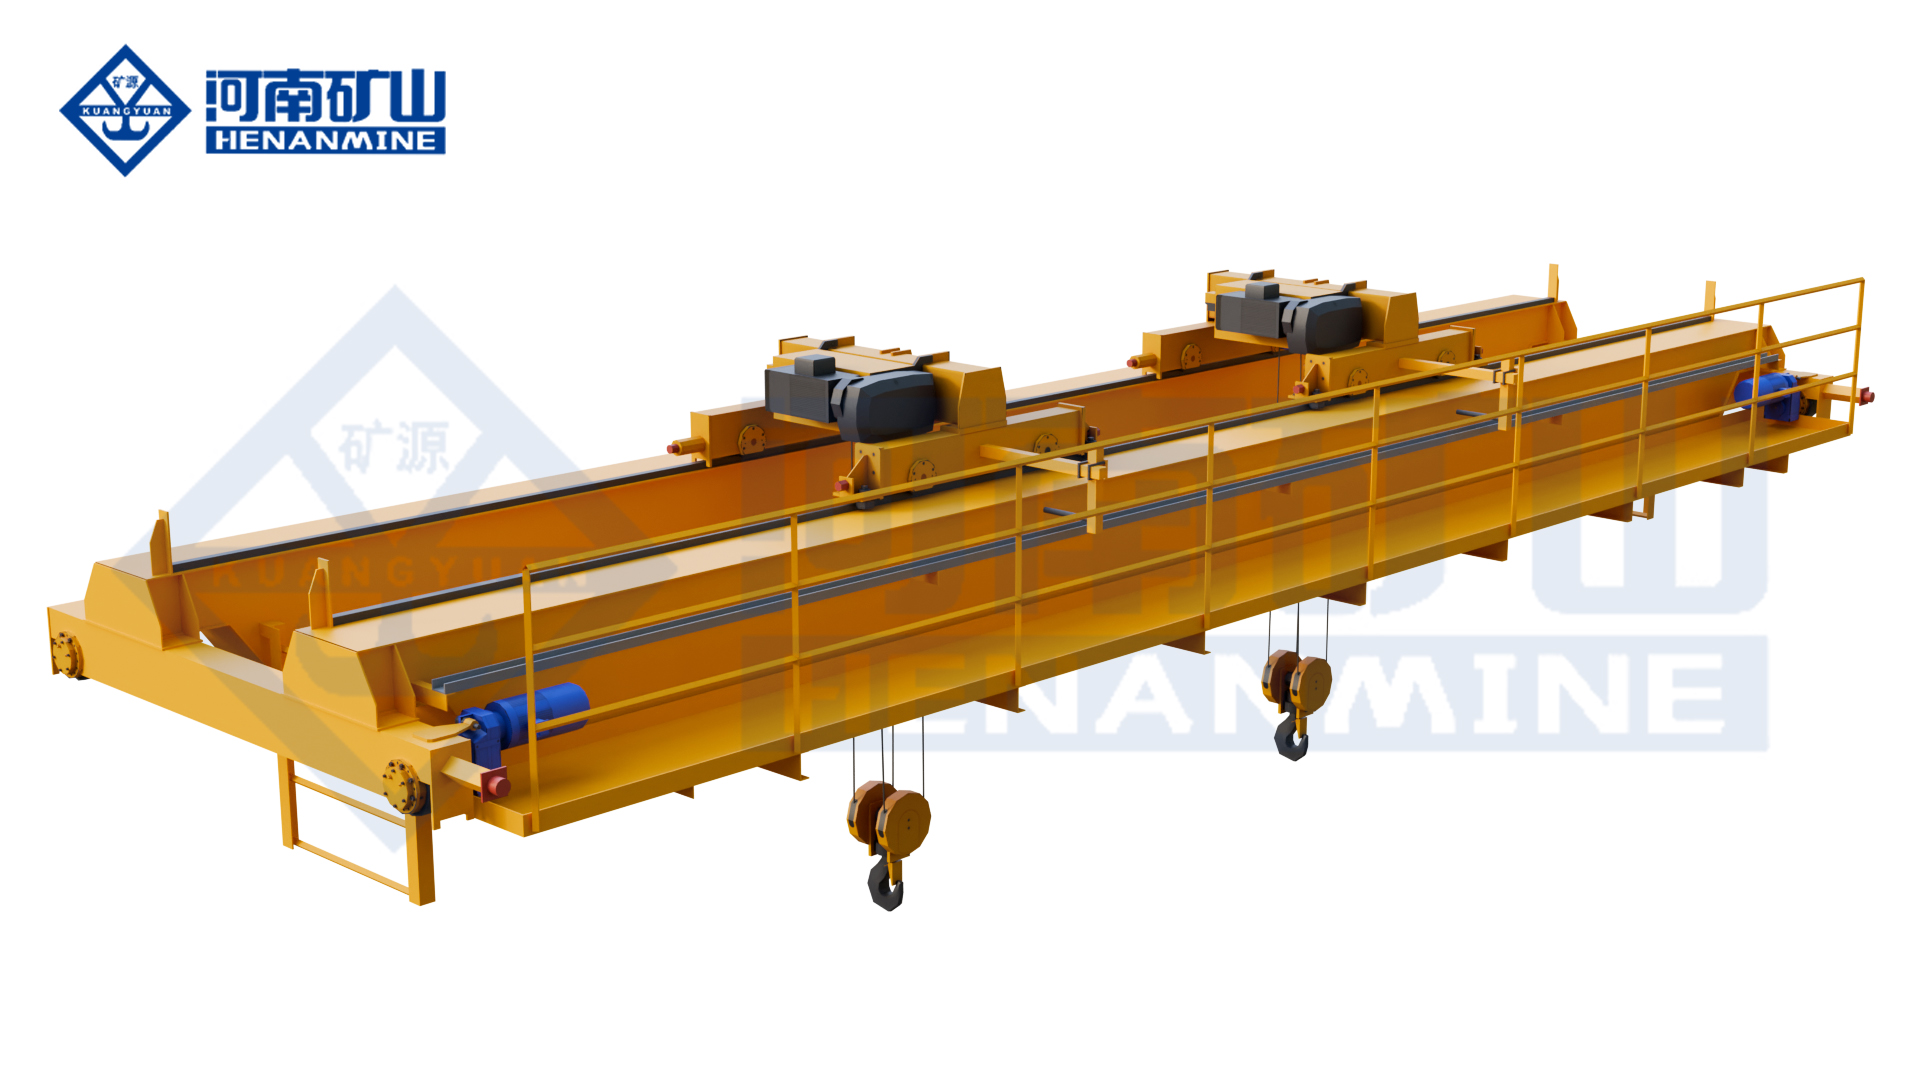
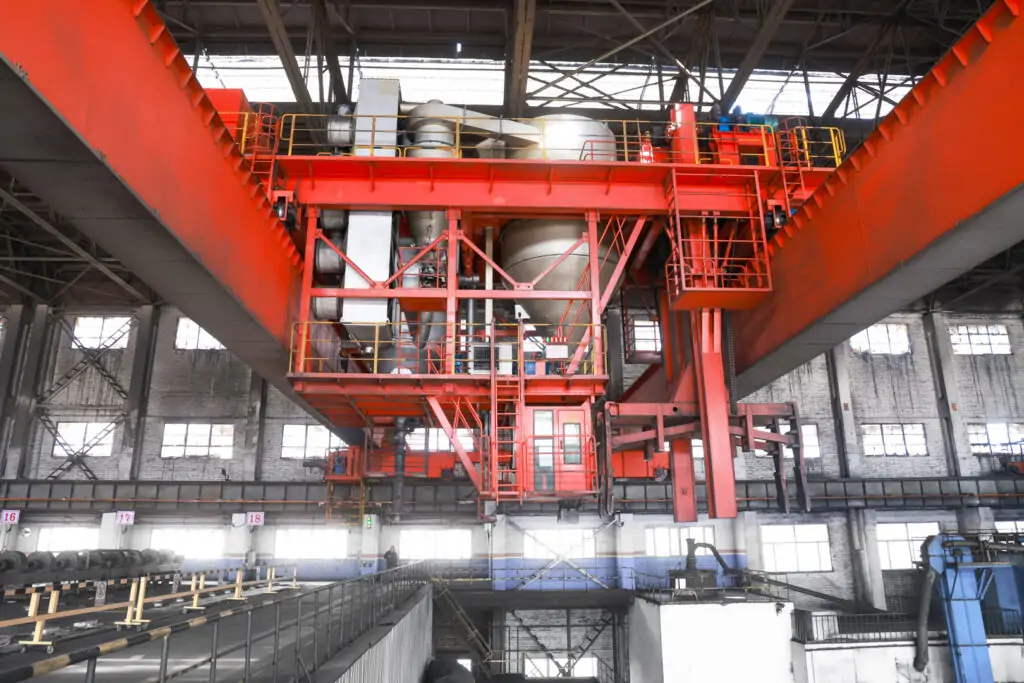
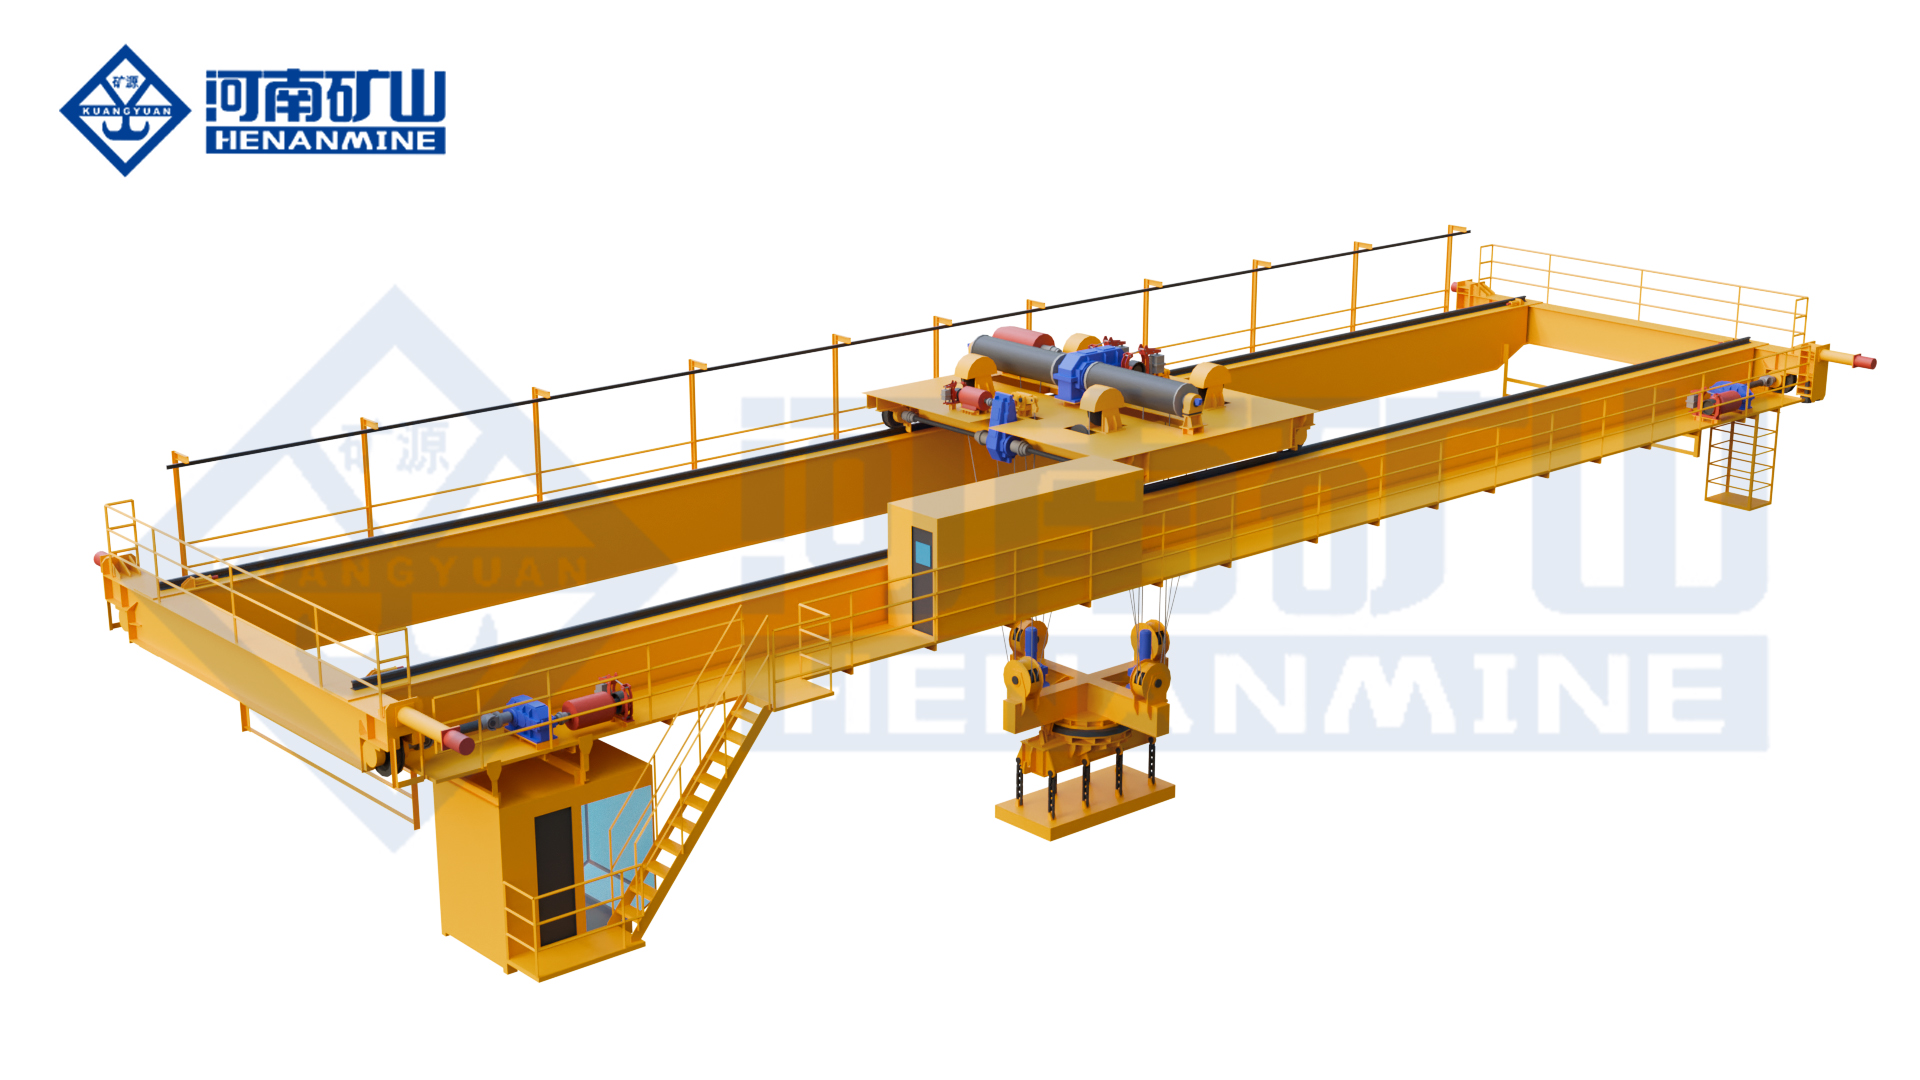
    coil handling crane platform with rotating electromagnetic hanging beam
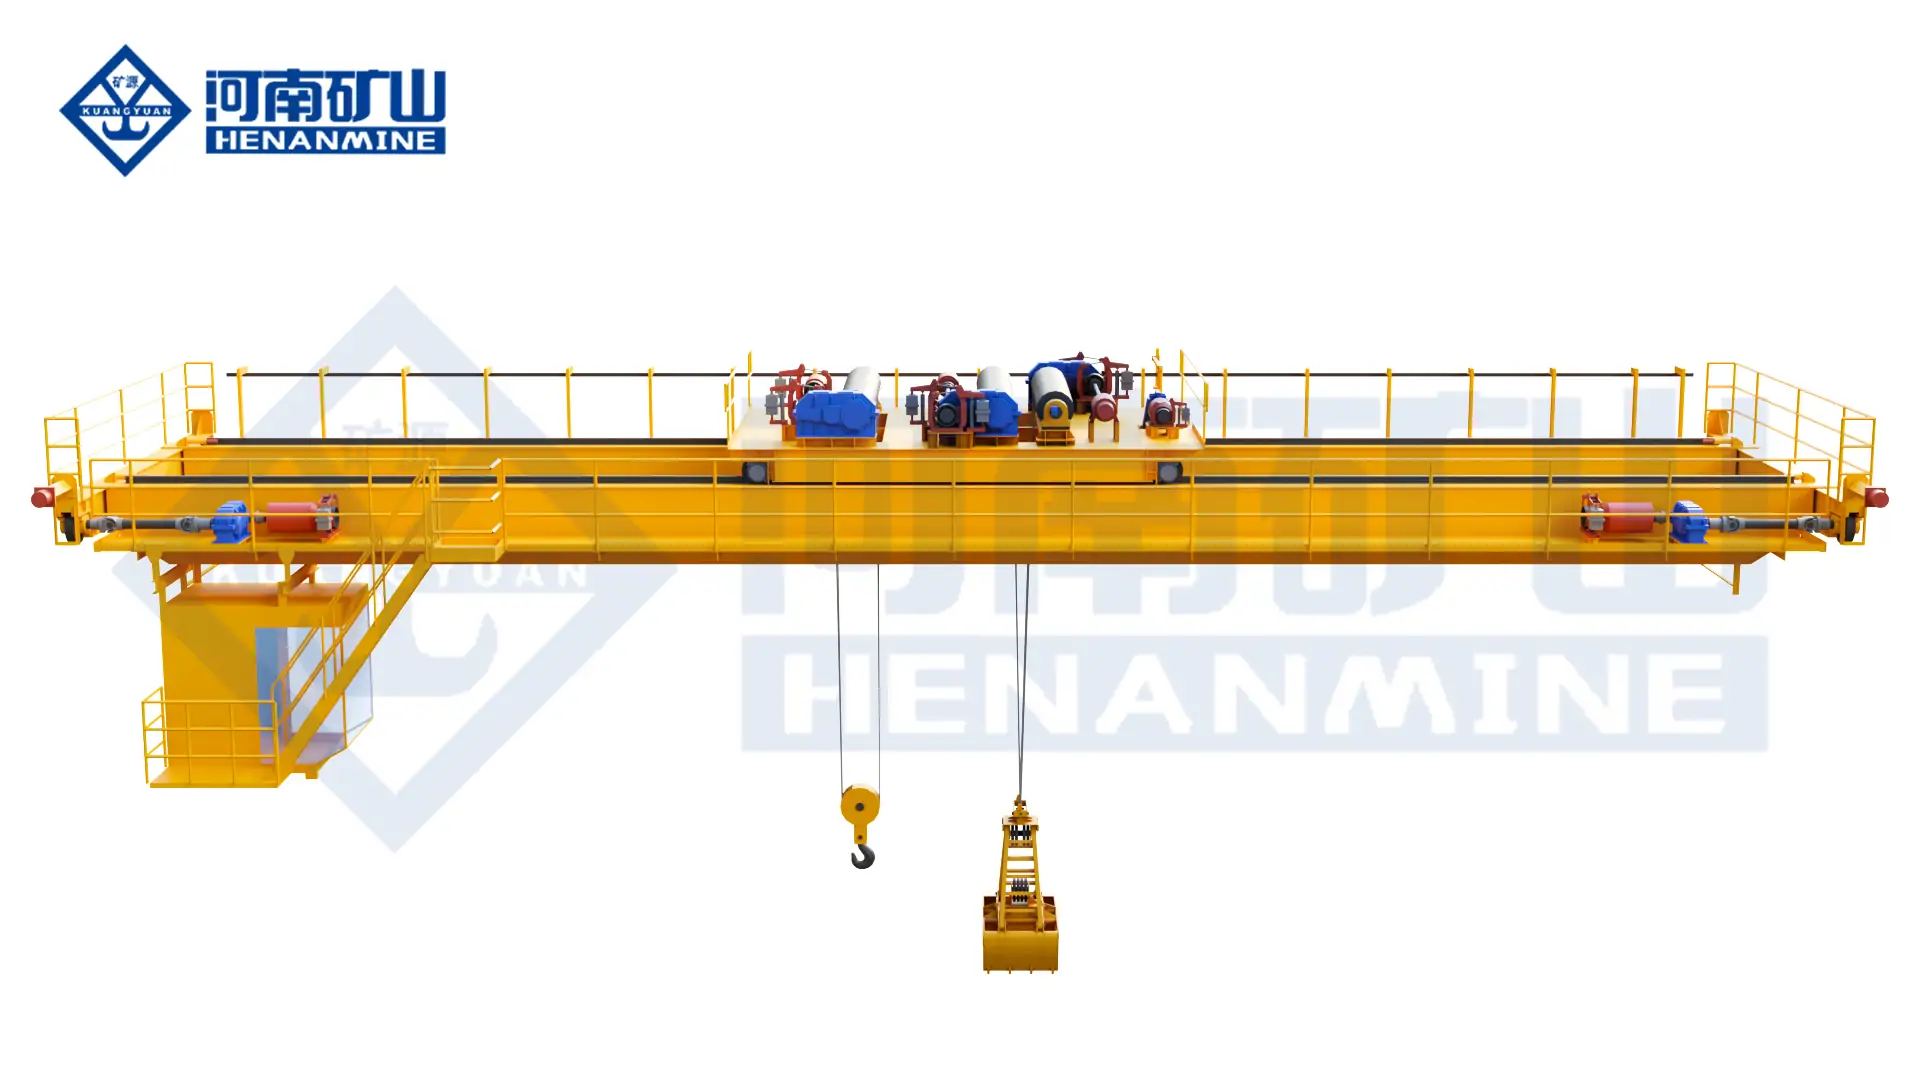
    A heavy-duty double-girder crane can be combined with a coil-specific C-hook, tong, mandrel or validated magnetic attachment.

    PRIMARY ARCHITECTURE

    Top-Running Double Girder

    COIL ATTACHMENTS

    C-Hook, Tong, Mandrel or Magnet

    OPERATING PROFILE

    Process-Defined Duty

    CONTROL OPTIONS

    Cabin, Radio, PLC & Automation

    What Is a Coil Handling Crane?

    A coil handling crane is an overhead process crane equipped to lift, transport, orient and place rolled metal coils. It is used in steel service centers, hot- and cold-rolling facilities, galvanizing and coating lines, slitting operations, aluminum plants, ports and finished-coil warehouses.

    The crane is only one part of the handling system. The coil attachment determines how the load is engaged, while the building, runway, storage saddles, process equipment and control system define the available approach and placement accuracy. A safe selection must consider the complete load path from pickup to final release.

    Coil mass alone is not an adequate design input. Outside diameter, inside diameter, face width, winding tightness, banding, eye orientation, material temperature, surface finish and center-of-gravity variation affect attachment geometry and stability. The attachment self-weight is included in the gross suspended load used to size the hoist, bridge, wheels and runway reactions.

    Henan Mine Crane combines customized coil attachments with double-girder bridge crane, metallurgical bridge crane and electromagnetic hanging crane platforms according to the confirmed process.

    Where Coil Handling Cranes Work

    The operating zone determines whether the priority is rapid unloading, gentle surface protection, accurate line feeding, high-density storage or automated order retrieval.

    Receiving and Unloading

    Unload coils from trucks, rail wagons or internal transfer cars. Vehicle clearances, side approach, securing-removal sequence and exclusion zones are coordinated with the crane lift path.

    Pickling, Rolling and Annealing

    Transfer coils between process lines, buffers and furnace areas. Heat, fumes, moisture, scale and restricted access influence component protection and maintenance arrangements.

    Slitting and Processing Lines

    Place master coils on uncoilers and remove finished coils or scrap reels. Low-speed positioning, approach limits and attachment clearance are coordinated with line equipment.

    Finished-Coil Warehouse

    Stack and retrieve coils by order, grade, width and destination. Position feedback, storage maps and inventory integration support higher storage density and traceability.

    Truck and Rail Dispatch

    Load coils into approved transport saddles or cradles. Loading sequence, vehicle identification and confirmation of stable placement are defined before release.

    Outdoor Coil Yard

    Outdoor gantry or bridge systems require wind, rain, corrosion, drainage, rail protection and parking or storm-restraint provisions in addition to coil-handling controls.

    A process map should identify every pickup position, coil orientation, storage saddle, line center, vehicle lane, personnel route and prohibited zone. It should also record the required cycle rate, queuing logic and production consequence of a crane outage.

    For plant-wide planning, steel mill crane systems should separate coil, plate, slab, scrap, roll-change, maintenance and molten-metal duties.
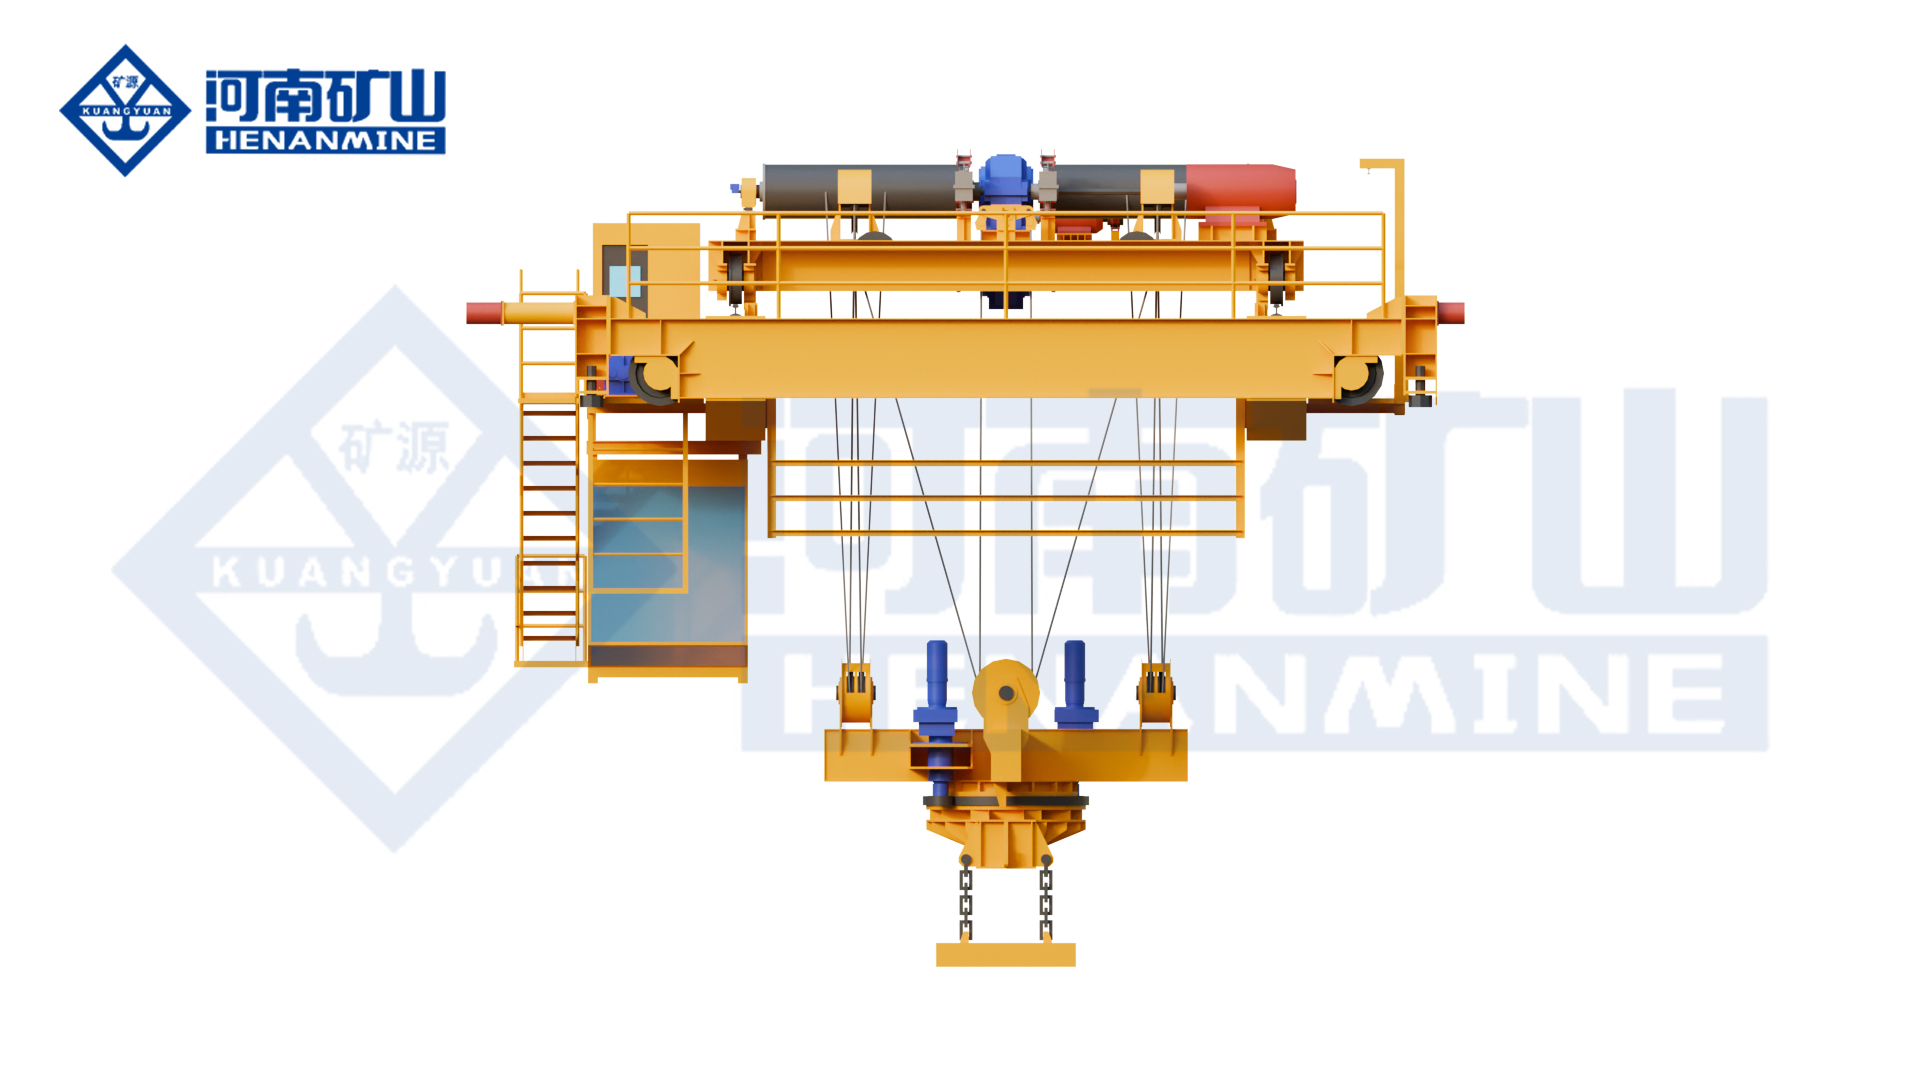
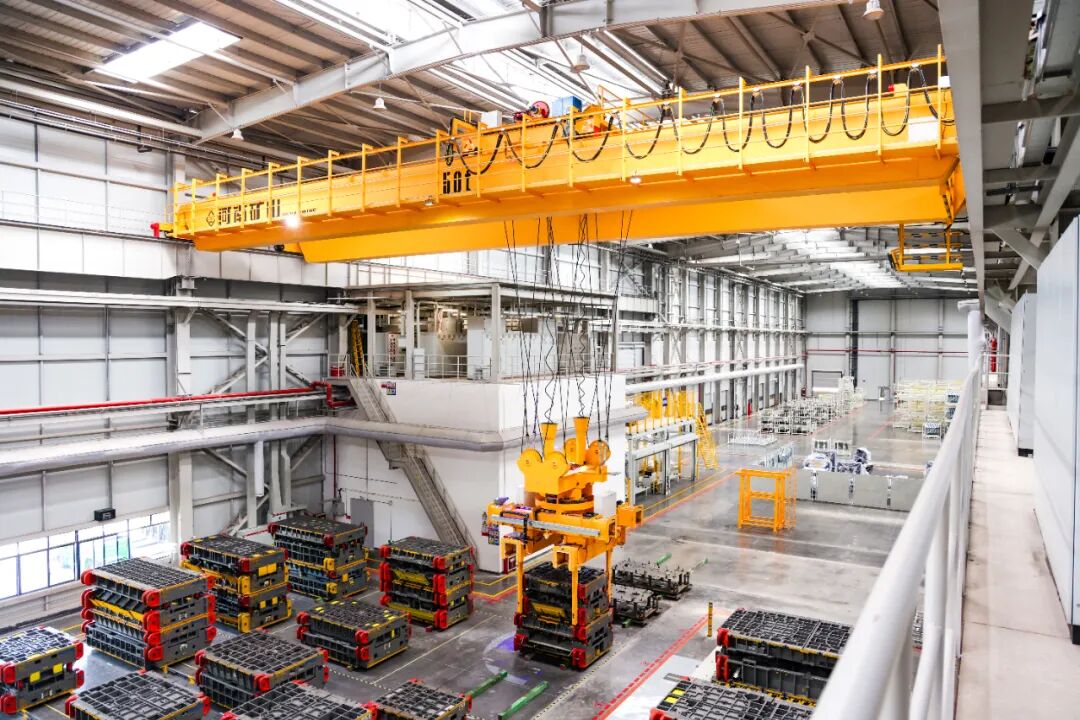
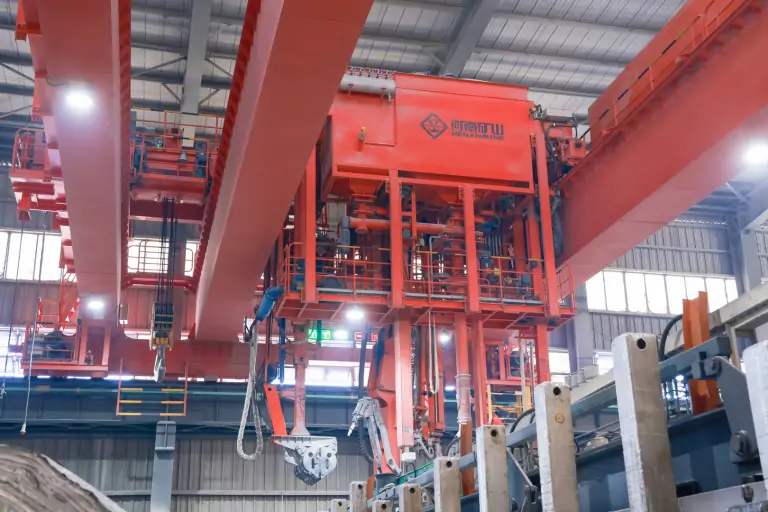
    rotating attachment arrangement on a heavy-duty coil handling crane platform
    Attachment geometry, rotation envelope and approach clearance are checked against every pickup and placement station.

    Components and Operating Principle

    The hoist raises the coil and attachment, the trolley positions the load across the bay and the bridge travels along the runway. Drives, brakes, encoders and controls coordinate these motions so the coil remains stable during pickup, transport and placement.

    Bridge and End Carriages

    Girders, diaphragms, wheels and travel drives are designed from span, duty, fatigue spectrum, wheel loads, lateral forces and runway stiffness.

    Process-Duty Hoist

    Drum, wire rope, sheaves, reducer, motor and brakes are selected for gross load, lift, speeds, starts per hour and the required reliability strategy.

    Coil Attachment

    C-hooks, tongs, inside-diameter lifters and approved magnetic systems engage different coil geometries. Attachment mass and center of gravity form part of the load case.

    Engagement Confirmation

    Limit switches, proximity sensors, load measurement, tong-position feedback or other validated devices establish a permissive before lifting.

    Variable-Speed Drives

    VFD-controlled hoisting and travel provide smooth acceleration, controlled creep speed and repeatable approach to storage saddles or process-line centers.

    Positioning and Data

    Encoders, laser positioning, cameras, barcode or RFID readers and warehouse interfaces can identify coils and confirm storage locations.

    Coil Handling Crane Selection Considerations

    Selection begins with the coil envelope and handling route rather than a nominal crane capacity. The following inputs define the crane, attachment and controls.

    Coil Geometry

    Minimum and maximum mass, outside diameter, inside diameter and face width; eye-horizontal or eye-vertical orientation; center-of-gravity variation; winding and banding condition.

    Material Condition

    Steel or aluminum grade, temperature, surface finish, coating, edge condition, permitted contact pressure and unacceptable marking or deformation.

    Duty and Throughput

    Lifts per hour, shifts, annual hours, load spectrum, travel distances, queue size, required cycle time and production consequence of an outage.

    Pickup and Placement

    Storage saddles, stack pattern, line mandrels, vehicle cradles, approach direction, insertion clearance, target tolerance and release confirmation.

    Building and Runway

    Rail-center span, runway length and elevation, lift, end and side approaches, roof clearance, existing wheel-load limits and installation access.

    Control and Integration

    Cabin, radio, semi-automatic or automatic operation; anti-sway; coil identification; WMS/MES protocol; traffic zones; manual fallback and recovery logic.

    Coil Handling Crane Configurations Compared

    The attachment is selected from the complete coil range and process route. No attachment is universally suitable for every coil.

    Configuration Suitable Handling Pattern Engineering Advantages Critical Controls
    C-Hook on Double-Girder Crane Eye-horizontal coils with accessible bore; receiving, storage and line feeding Simple load path, no powered gripping mechanism and clear visual engagement Hook-arm length, counterbalance, coil-width range, tip clearance, protective pads and approach space
    Motorized Coil Tong or Clamp Crane High-cycle warehouses, automatic pickup and restricted manual access Powered engagement, coil-width adjustment and positive status feedback Contact pressure, open/closed indication, mechanical retention, release interlock and edge protection
    Inside-Diameter or Telescopic Mandrel Lifter Coils with controlled bore dimensions where outside surfaces must remain unobstructed Internal engagement and reduced contact with finished outer surfaces Inside-diameter tolerance, expansion confirmation, insertion depth, core strength and release prevention
    Electromagnetic Hanging Crane Only validated ferromagnetic coils and material geometries within the approved magnetic operating envelope Non-rigged pickup and possible rotation or automated material identification Material grade, temperature, contact area, air gaps, banding, residual magnetism, backup strategy and release control
    Hook, Beam and Sling Arrangement Low-frequency handling, maintenance lifts or exceptional coils with engineered lifting points Flexible rigging for unusual loads without a permanent powered attachment Approved lift plan, sling protection, angle effects, manual access and secure connection

    An automatic attachment can improve throughput, but it also adds sensors, powered motion, inspection points, control logic and recovery procedures. The complete lifecycle and outage consequence should be compared with the simplicity of a C-hook.

    Coil Handling Crane Technical Specification Framework

    Final values are confirmed on the approved technical schedule. Published product-family positions support preliminary configuration but do not establish a guaranteed combination.

    Specification Item Required Input Engineering Output Contract Evidence
    Rated load Maximum coil plus attachment, block and all below-hook equipment Crane rated load and permitted attachment combinations Load schedule and nameplate basis
    Span, lift and approaches Runway drawings, rail centers, elevations and clearance survey General arrangement and hook or attachment coverage Approved GA drawing
    Duty classification Load spectrum, cycles, starts, shifts and annual hours Crane and mechanism classifications Duty calculation and design basis
    Motion performance Cycle target, travel distances and placement tolerance Main and creep speeds, acceleration and braking profiles Drive schedule and witnessed cycle test
    Attachment envelope OD, ID, width, orientation, temperature and surface limits Permitted coil matrix and attachment settings Attachment data sheet and operating limits
    Runway reactions Building capacity, rail and support structure Maximum/minimum wheel loads and horizontal forces Reaction schedule for civil approval
    Control and automation Operating modes, location accuracy, WMS/MES messages and safety zones Control narrative, I/O, interfaces and fallback mode Functional specification and acceptance test

    Published Henan Mine Crane Reference Platforms

    Product Platform Published Position Possible Coil-Mill Role Application Boundary
    Electromagnetic Hanging Crane 5–50 t; 10.5–31.5 m span; 6–20 m lift; A6–A7 Rotating metal-material handling where magnetic pickup is validated Coil grade, geometry, air gap, temperature and retention strategy require project approval
    Electromagnetic Bridge Crane 5–32 t including attachment; 10.5–31.5 m span; 6–30 m lift Ferromagnetic material transfer and compatible unit loads Final duty and magnet system are process-defined
    Metallurgical Bridge Crane 5–50 t; 7.5–35 m span; 6–20 m lift; A6–A7 Coil handling in specified high-duty or steel-production environments Attachment, temperature and production role define the final platform
    Custom C-Hook or Coil-Tong Crane Project-defined capacity, span, lift, duty and speeds Dedicated coil receiving, line feeding, warehousing and dispatch Final configuration follows the approved coil matrix and process map

    Coil Attachment Engineering and Surface Protection

    The attachment must control the coil without crushing the core, marking finished surfaces, opening the winding or allowing the load to migrate. Pads, shoes, hook arms and contact faces are selected from the declared material and surface limits.

    Representative-coil testing is required whenever engagement depends on bore size, contact friction, magnet performance, tong pressure or automated recognition. A suspended dead weight does not reproduce every real coil condition.
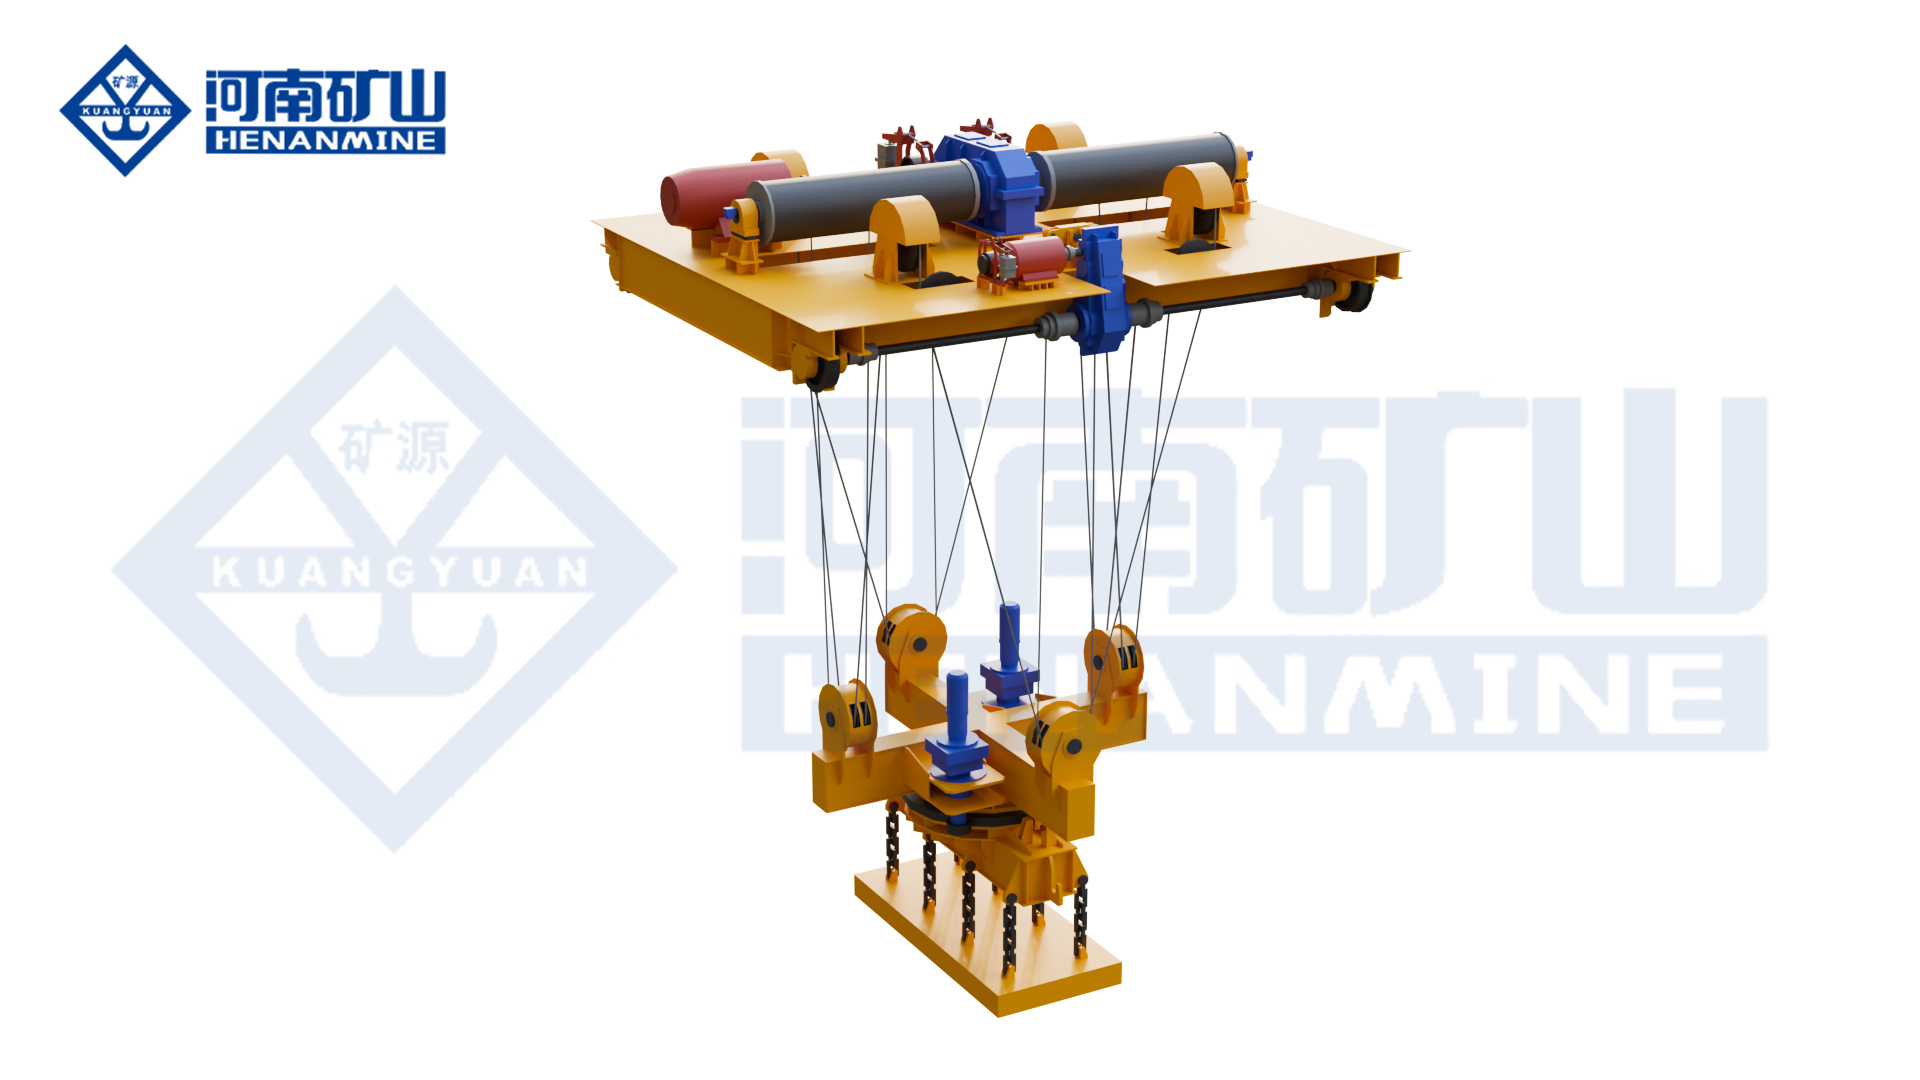
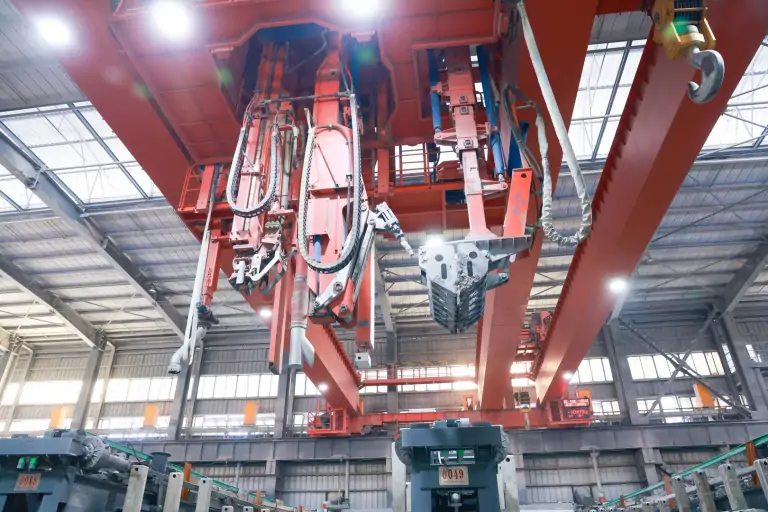
    coil handling crane attachment and rotating beam engineering
    Rotation, engagement and release functions are interlocked with the permitted load envelope and safe clearance zone.

    C-Hook Design

    Hook opening, arm length, back height, counterbalance, protective lining, tip shape and rated-load marking are matched to the full ID, OD and width range. The approach path must allow complete insertion without striking the bore or adjacent coils.

    Coil Tong Design

    Powered tongs require an approved gripping-force range, contact geometry, open/closed feedback, mechanical retention and release prevention while suspended. The control system must identify an incomplete or off-center engagement.

    Inside-Diameter Lifter

    Mandrel expansion, insertion depth and engagement confirmation are designed around bore tolerance and core strength. The lifter must not release until the coil is supported at the approved destination.

    Magnetic Attachment

    Magnetic handling is considered only after grade, temperature, air gaps, curvature, banding and contact area are validated. The design defines monitoring, backup retention or power strategy, alarms and controlled release.

    Load Stability, Safety Functions and Storage Interfaces

    A coil can roll, telescope, unwind or shift if the attachment, storage saddle or transport acceleration is wrong. Safety functions are therefore defined from the complete operating sequence.

    Control Purpose Design Inputs Acceptance Evidence
    Load and overload protection Prevent lifting beyond the approved gross suspended load Coil and attachment combinations, dynamic effects and calibration range Calibration and functional test records
    Engagement permissive Block hoisting until the attachment is correctly positioned Sensor coverage, false-positive cases and manual recovery Representative pickup trials
    Release interlock Prevent opening or demagnetizing while the coil is suspended Supported-load detection, release sequence and override authority Witnessed normal and failure-mode tests
    Anti-sway and motion limits Control swing and prevent collision with coils, equipment or building structures Load dependence, clearances, stop distance and fallback mode Approach, braking and repeatability tests
    Restricted-area protection Separate suspended coils from personnel, vehicles and process equipment Zone map, scanners, barriers, warning devices and bypass control Zone validation and stop tests
    Saddle and stack confirmation Confirm stable support before attachment release Saddle geometry, coil orientation, stack rules and acceptable location tolerance Placement trials across the approved coil range

    Operating boundary: side pulling, dragging a coil, lifting an unsecured or visibly damaged coil, standing within the roll path and releasing an attachment before stable support are excluded unless a documented engineered procedure specifically permits the condition.

    Manual, Semi-Automatic and Automatic Coil Handling

    Automation level should follow repeatability, traffic risk, production throughput, coil identification quality and the ability to maintain sensors and software.

    Control Level Typical Functions Appropriate Conditions Required Definition
    Manual control Cabin or radio control, variable speeds, load display, cameras and interlocks Variable tasks and experienced operator supervision Sightlines, operator location, communication and safe access
    Semi-automatic Automatic positioning or anti-sway with operator-authorized pickup and release Repeated stations with occasional exceptions Handover points, confirmation logic and exception recovery
    Fully automatic Task receipt, coil recognition, pickup, transport, storage, retrieval and completion feedback Controlled warehouses with stable data, defined zones and standardized coil conditions WMS/MES protocol, coordinate system, safe-state logic, cybersecurity and manual fallback

    Coil Identification

    Barcode, RFID, production data or machine vision associates each coil with mass, dimensions, grade, order and storage location.

    Positioning and Anti-Sway

    Absolute or incremental position feedback, target coordinates and load-dependent anti-sway support repeatable pickup and placement.

    Inventory Integration

    The interface defines task ownership, material identity, destination, status, alarms, time synchronization and recovery after communication loss.

    Design Basis, Inspection and Acceptance

    The purchase specification identifies one coherent design basis. Local statutory requirements remain applicable at the installation site, and standards from different systems are not combined selectively without an approved compliance matrix.

    Possible Design Routes

    A project may use the ISO 4301 classification framework with applicable crane and electrical standards, the EN 13001 series with EN 15011 and relevant lifting-attachment requirements, or a North American route using CMAA specifications with applicable ASME B30 requirements. The contract states the selected basis.

    Engineering Deliverables

    General arrangement, wheel loads, duty basis, coil matrix, attachment data, clearance study, electrical drawings, control narrative, interface list, inspection plan and maintenance-access arrangement.

    Manufacturing Inspection

    Material identification, welding procedure and welder qualification, specified NDT, dimensional checks, attachment inspection, machinery alignment, panel inspection and coating records.

    FAT and Site Acceptance

    Functional tests verify motions, limits, brakes, interlocks, attachment engagement, alarms and available automation before shipment. Site testing then covers runway, erection, load testing, representative-coil trials, interfaces, training and handover.

    Relevant Steel-Mill and Automation Experience

    Project references are evaluated by process similarity. The following Henan Mine Crane projects demonstrate metal-material automation and coordinated crane planning. A coil attachment is still engineered from the new project’s coil matrix.
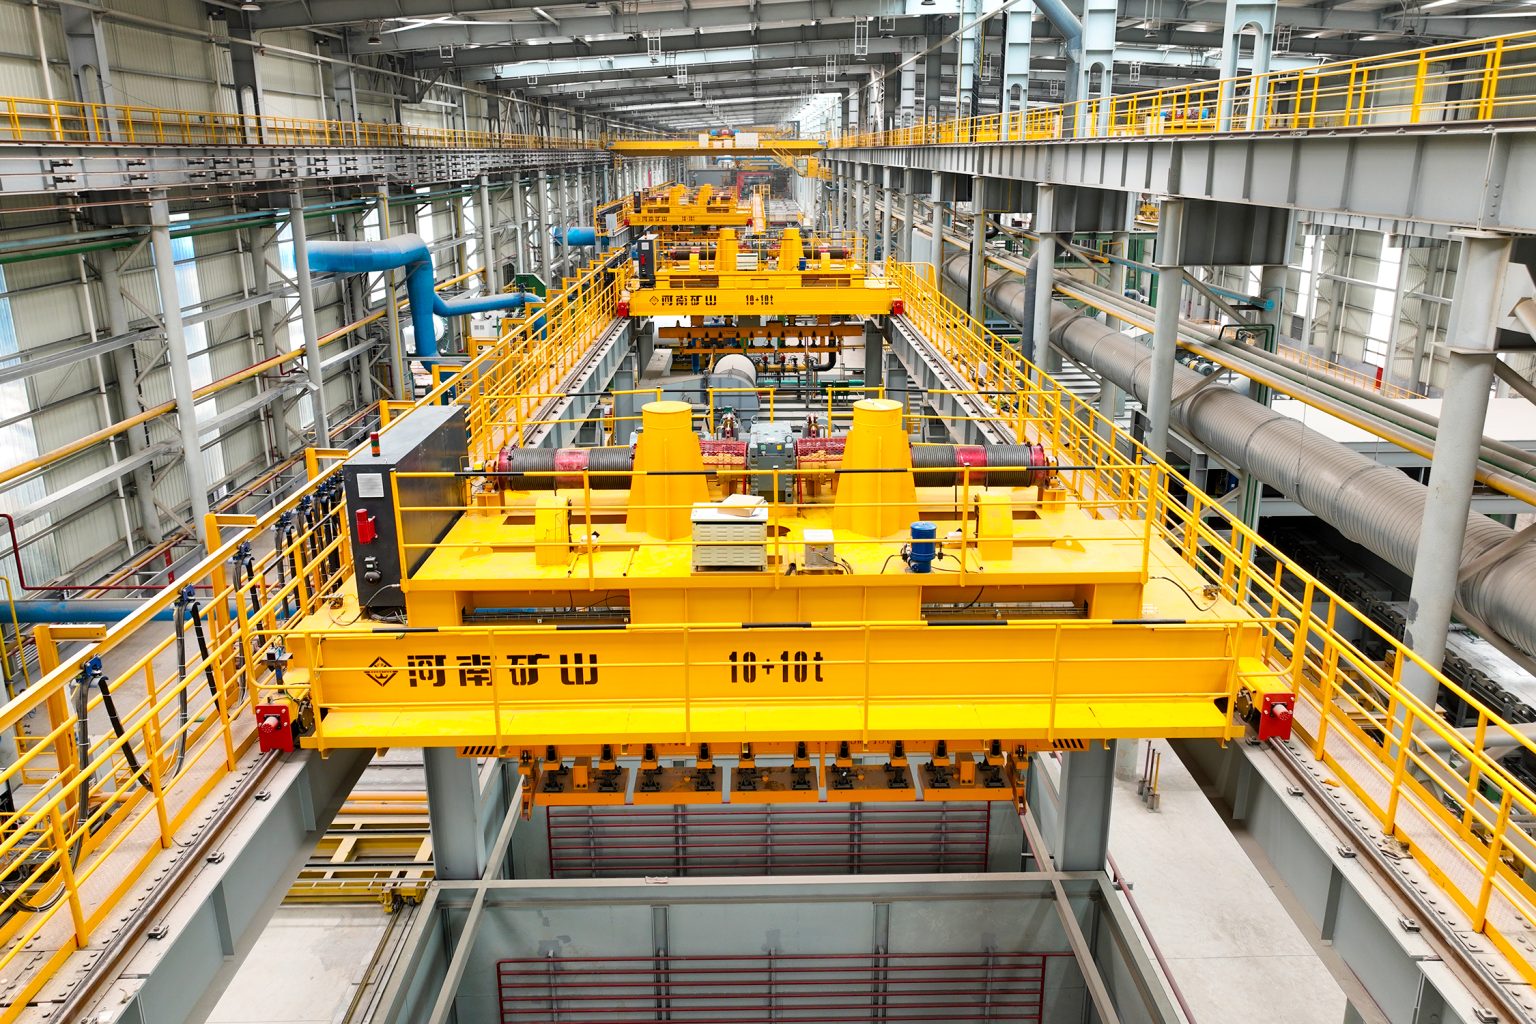
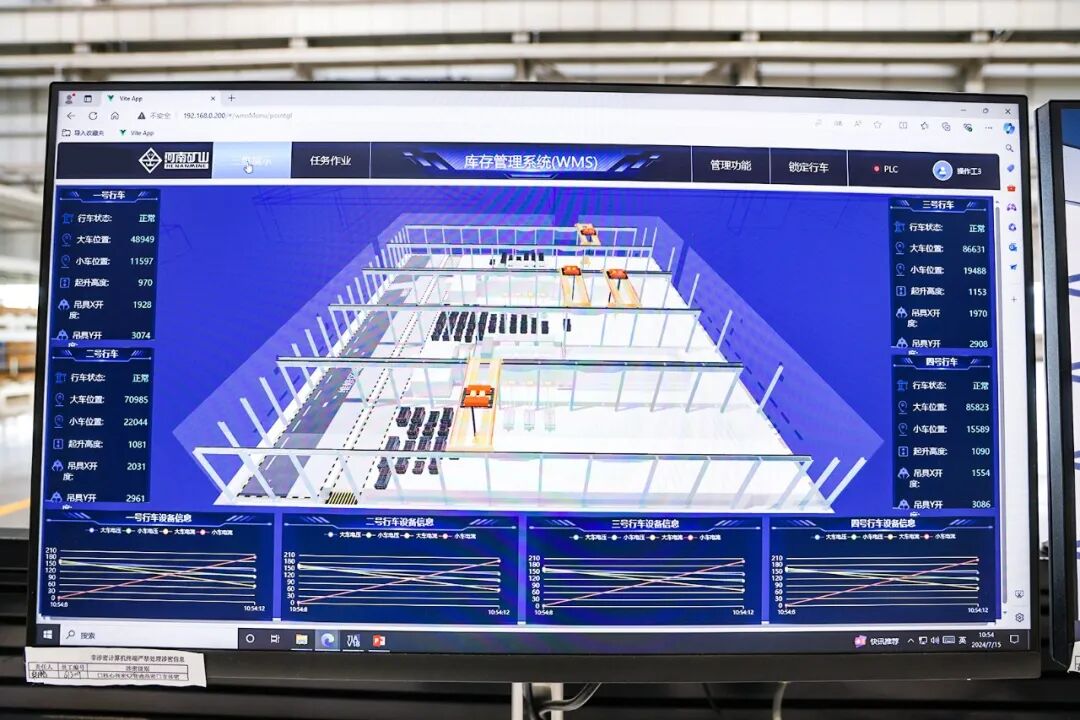
    Henan Mine Crane automatic electromagnetic hanging girder crane

    Metal-Material Automation Reference

    Automatic Electromagnetic Hanging Girder Crane

    The published project supports MES connection, unattended material transfer, automatic avoidance and nearby scheduling for cranes sharing a bay.

    These control principles are relevant to automatic coil warehouses, while the coil-recognition method, attachment and release logic remain project-specific.
    View Automation Reference

    Henan Mine Crane hot rolling mill crane fleet project

    Steel-Mill Fleet Reference

    34 Cranes for a 4.5-Million-Tonne Plate Facility

    Henan Mine Crane supplied 34 double-girder overhead cranes rated from 10 t to 100 t for production, roll handling, tooling, equipment service and maintenance.

    The reference demonstrates process-based fleet planning: coil receiving, line feeding, warehousing and maintenance can require different capacities, speeds and control levels.

    View Steel-Mill Reference

    Reference boundary: these projects demonstrate relevant crane engineering and automation capability; they do not establish the final capacity, attachment or performance of a new coil handling crane.

    Coil Handling Crane Price and Budget Scope

    A responsible coil handling crane price requires the coil range, attachment, capacity, span, lift, duty, speeds, controls, runway scope and destination. Public prices are useful only as preliminary market signals.

    Public Market Signal Checked in September 2026 Published Position What It Indicates Commercial Limitation
    Generic 50 t double-girder overhead crane guide Approximately US$9,800–110,000 Capacity alone permits a very wide equipment range No normalized coil attachment, duty, controls, runway, delivery or commissioning scope
    10 t C-hook or clamp-tong coil crane listing US$35,000–140,000 published FOB range A coil-specific attachment and heavy-duty crane can materially change budget Listing does not define a fully comparable attachment, duty, testing, freight or installation boundary
    30 t heavy-duty clamp coil crane listing Price on request Specialist suppliers often require project data before pricing Published attributes do not establish an installed project price
    Automatic coil warehouse crane Project quotation Price is built from crane, attachment, positioning, safety zones and software interfaces A complete functional specification and site boundary are required

    Major budget drivers: maximum gross load; span, lift and approaches; working class; C-hook, tong, mandrel or magnetic package; coil-recognition system; anti-sway and positioning; WMS/MES integration; cabin and environmental protection; runway and electrification; export packing, freight, erection, tests and local compliance.

    The published figures are public market observations, not Henan Mine Crane offers. Marketplace prices may be placeholders or equipment-only values. Contract comparisons require a line-by-line technical and commercial scope reconciliation.

    Coil Handling Crane RFQ Information

    A complete enquiry allows the crane, attachment, runway reactions, controls and commercial scope to be priced on the same basis.

    Coil Data

    Material and grade; minimum and maximum mass, OD, ID and width; eye orientation; temperature; surface condition; banding; center of gravity; permitted contact marks; drawings or photographs.

    Process and Duty

    Pickup and placement stations; storage pattern; cycle sequence; lifts per hour; shifts; annual hours; load spectrum; travel distances; target cycle time; outage consequence.

    Building and Runway

    Span, runway length, rail section and elevation; required lift; approaches; clearances; existing wheel-load limits; runway drawings; installation access and site survey.

    Controls and Commercial Scope

    Manual or automatic operation; positioning tolerance; WMS/MES protocol; safety zones; voltage and frequency; environment; destination; design standard; Incoterm; installation, testing and documentation scope.

    Frequently Asked Questions

    How is coil handling crane capacity calculated?

    The starting point is the maximum gross suspended load: coil plus C-hook, tong, mandrel, magnet, hook block and every other item below the hoist. Duty, load distribution and dynamic effects are then applied under the selected design standard.

    Is a C-hook or coil tong better?

    A C-hook is mechanically simple and effective where the coil bore is accessible. A powered tong supports automated engagement and variable widths but adds mechanisms, sensors and maintenance. Coil geometry, cycle rate, access and automation level determine the selection.

    Can magnets safely lift steel coils?

    Only when the steel grade, coil geometry, contact area, temperature, air gaps, banding and retention strategy have been validated. A magnetic system cannot be assumed suitable from coil mass alone.

    Can one attachment handle the full coil range?

    It is possible only when every OD, ID, width, mass, orientation and surface condition falls within the approved envelope. Wide ranges may require adjustable or interchangeable attachments and dedicated storage stands.

    How much does a coil handling crane cost?

    Public information reviewed in September 2026 included approximately US$9,800–110,000 for a generic 50 t double-girder price guide and US$35,000–140,000 for one 10 t C-hook or clamp-tong coil-crane listing. A final price requires the approved crane, attachment and project scope.

    Can an existing runway be reused?

    Only after rails, beams, columns, brackets, connections and foundations are checked for condition, alignment, fatigue and the new crane reactions. The crane must remain within verified structural limits or the runway must be strengthened.

    Can the crane connect to WMS or MES?

    Yes. The interface specification defines tasks, coil identity, coordinates, inventory status, protocol, time synchronization, safety boundaries, cybersecurity, manual override and recovery after a network interruption.

    What should be tested before handover?

    Testing covers crane motions, brakes, limits, load protection, attachment engagement and release, representative coils, placement tolerance, safety zones, failure responses, interfaces and manual recovery under agreed acceptance criteria.

    Request a Coil Handling Crane Quote

    Submit the coil mass and dimension range, eye orientation, temperature, surface condition, required attachment, handling cycle, span, lift, runway data, control level, power supply, destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.
    Henan Mine CraneDiscuss your requirements ↗
  • Cement Plant Crane

    Cement Plant Crane

    Cement Plant Crane

    Henan Mine Crane · Cement Production Lifting Systems

    Cement Plant Crane

    Engineered overhead, grab and gantry crane systems for raw-material storage, fuel handling, kiln and mill maintenance, clinker and additive transfer, workshops and outdoor service areas.

    Henan Mine Crane configures each cement plant crane around the handled material or maintenance load, process area, required throughput, crane duty, dust and temperature conditions, plant layout, automation level and contractual supply boundary.

    Henan Mine Crane intelligent grab double-girder overhead crane for cement plant bulk material handling
    A cement plant lifting system is selected by process duty: bulk-material cranes and maintenance cranes require different structures, attachments and controls.

    Core duties
    Bulk transfer and process-equipment maintenance

    Primary systems
    Grab, hook, dual-purpose and gantry cranes

    Critical inputs
    Material data, load, throughput, duty and environment

    Commercial basis
    Defined technical scope and project quotation

    Crane Systems for Cement Production and Maintenance

    A cement plant crane is not one standardized machine. Raw-material and fuel stores may require a high-duty grab crane for stockpiling, blending, reclaiming or feeding a hopper. Kiln, crusher, cooler, raw-mill and cement-mill buildings require hook cranes or hoists for planned maintenance of motors, gearboxes, rollers, fans and other process components. Outdoor equipment yards may require a rail-mounted gantry crane.

    Continuous production flow is normally served by conveyors, elevators and dedicated process equipment. A grab crane should therefore be specified only where the plant layout includes a storage bay, pit, bunker or transfer point that benefits from crane coverage. Its design must be based on material bulk density, particle size, moisture, abrasiveness, angle of repose, required tonnes per hour and receiving-hopper geometry.

    Cement dust alone does not automatically make an area explosion hazardous. Coal, petroleum coke and some alternative-fuel areas may be classified for combustible dust, but the required equipment group, zone or division, temperature class and protection concept must come from the plant hazardous-area documentation. High-temperature protection is likewise applied from measured ambient and radiant-heat conditions, not from the industry name.

    Cement Plant Crane Configurations

    01 · Intelligent Grab Overhead Crane

    A double-girder, four-rope grab system for repeated handling of limestone, clay, gypsum, slag, clinker, coal or other approved bulk materials. PLC control, pile scanning, anti-sway, positioning and plant-system interfaces can support semi-automatic or unmanned operation.

    02 · Grab-and-Hook Dual-Purpose Crane

    A practical mixed-duty solution where one bay handles both bulk material and unit loads. The design must define attachment changeover, rated load in each operating mode, storage position and controls that prevent an invalid configuration.

    03 · Double-Girder Maintenance Crane

    A hook crane for heavy process-equipment maintenance in kiln, cooler, crusher, fan, raw-mill and cement-mill buildings. Main and auxiliary hooks, low-speed positioning and maintenance access can be configured around the overhaul method.

    04 · Single-Girder Service Crane

    An economical option for lighter maintenance, workshop, packing-line and utility-building loads where the verified capacity, span, headroom and operating frequency remain within the selected hoist and runway design.

    05 · Double-Girder Gantry Crane

    A rail-mounted outdoor crane for equipment yards, maintenance laydown areas and construction or shutdown support where the building cannot provide an overhead-crane runway. Wind, rails, foundations and storm parking are integral design requirements.

    06 · Hazardous-Area Crane or Hoist

    A certified configuration for a documented combustible-dust or gas classification, such as a defined coal or alternative-fuel zone. Motors, brakes, electrics, controls, cable systems and mechanical interfaces must match the approved classification.

    Compare Cement Plant Crane Options

    The correct configuration follows the task, process zone and operating cycle. A high-speed grab crane selected for bulk throughput is not an economical substitute for an occasional maintenance crane, while a general-purpose hoist is not designed for continuous stockyard reclaiming.

    Configuration Best-matched duty Principal advantage Procurement constraint
    Intelligent grab crane High-cycle bulk storage, blending and hopper feeding Large bay coverage with automated material-flow options Requires verified material data, throughput model, pile geometry and interface logic
    Grab-and-hook crane Mixed bulk and maintenance loads in one bay Two handling modes from one runway system Changeover time and lower specialization may not suit continuous bulk duty
    Double-girder hook crane Kiln, mill, crusher, cooler and fan maintenance High load, hook-height and auxiliary-hook flexibility Building runway, hook approaches and equipment-removal routes must be coordinated
    Single-girder service crane Light and medium intermittent maintenance Lower equipment and building loads for suitable duties Limited for heavier equipment, demanding duty or complex hook arrangements
    Rail-mounted gantry crane Outdoor equipment and shutdown laydown areas Independent of the process-building roof structure Foundations, rails, wind actions, parking and site traffic are part of the system

    Select Capacity, Grab Volume and Duty from Actual Work

    For a hook crane, rated capacity must cover the heaviest maintainable component together with the hook block, lifting beam, slings, shackles and every item suspended below the hook. The removal path should confirm centre of gravity, lifting points, required headroom, hook approach and the load position that creates the governing wheel reactions.

    For a grab crane, crane capacity includes the grab self-weight plus the material payload. Required grab volume follows the target payload, loose bulk density and realistic fill factor. Dense clinker, abrasive slag, fine powder and low-density alternative fuel can require different grab geometry even when the nominal volume is identical.

    Working class is calculated from operating hours, starts per hour, load spectrum, travel distances and expected service life. Production tonnes per hour must be checked through a cycle model covering closing, hoisting, trolley travel, bridge travel, discharge, return travel and expected process delays.

    Cement Process Area and Crane Selection Matrix

    Process area Typical handling requirement Crane-system priorities
    Raw-material storage Limestone, clay, corrective materials and additives in a defined bay or pit Grab suitability, pile scanning, hopper interface, dust protection and throughput
    Coal, petcoke or alternative fuel Stockpiling, mixing, reclaiming or feeding where a crane-based process is selected Hazardous-area classification, fire strategy, material variability and remote operation
    Crusher and raw mill Removal of motors, gearboxes, rollers, liners and drive components Hook approaches, maintenance openings, low-speed control and equipment laydown
    Kiln, preheater and cooler Planned shutdown lifting of fans, drives, refractory-service equipment and assemblies Measured heat exposure, lifting route, outage criticality and maintenance access
    Clinker and additive storage Approved bulk handling or reclaiming duty within storage structures Temperature at pickup, abrasion, dust containment and receiving-point control
    Cement grinding Mill, separator, motor, gearbox and fan maintenance Capacity from component schedule, accurate positioning and building clearance
    Packing and dispatch Maintenance of packers, palletizers, loaders and auxiliary machinery Compact headroom, safe access and coordination with logistics traffic
    Workshop and outdoor yard Repair, assembly, spare-parts handling and shutdown staging Overhead or gantry layout, weather protection, rails, foundations and traffic separation

    Technical Specification for a Cement Plant Crane

    Final values are established from process data, maintenance schedules, plant and civil drawings, site conditions and destination requirements. The following information creates a comparable technical proposal.

    Specification item Project definition
    Crane duty Bulk handling, maintenance, dual-purpose service, construction support or outdoor yard duty
    Rated capacity Grab plus payload for bulk duty; complete suspended maintenance load including rigging for hook duty
    Material and attachment Bulk density, size, moisture, abrasion and flow behavior; four-rope, hydraulic or sealed grab as applicable
    Span and travel length Building bay or rail gauge, runway length, end approaches, maintenance positions and pile coverage
    Lifting height Lowest pickup, top of pile, receiving hopper, highest obstruction and required maintenance clearance
    Duty and throughput Load spectrum, starts per hour, shifts, annual cycles, average and peak tonnes per hour
    Speeds and positioning Hoisting, trolley and bridge speeds; acceleration, creep speed, anti-sway and stopping accuracy
    Control and automation Pendant, radio or cabin; PLC, pile scanning, positioning, collision avoidance and DCS/MES interface scope
    Environment Ambient and radiant temperature, dust loading, humidity, corrosivity, altitude, wind and indoor/outdoor exposure
    Hazardous-area data Area classification, material characteristics, equipment group/category, temperature class and certificate requirements
    Runway and civil interface Rail profile, support spacing, allowable wheel loads, foundation data, access, drainage and erection route
    Electrical supply Voltage, phase, frequency, power-feed method, earthing and permitted variation
    Codes and acceptance Destination regulations, agreed design standard, inspection plan, testing, documentation and functional acceptance criteria

    Controls, Safety and Cement-Plant Environment

    Dust-Resistant Design

    Protected electrical enclosures, sealed or guarded components, suitable bearings, cable systems and accessible cleaning points are selected from the actual dust exposure and maintenance regime.

    Heat Assessment

    Equipment near kiln or clinker areas may require thermal shielding, heat-resistant components, cooling or derating after ambient and radiant temperatures are established.

    Hazardous-Area Compliance

    Explosion-protected equipment is applied only to a documented classified zone. The complete crane, not merely the hoist motor, must match the agreed protection concept.

    Intelligent Bulk Control

    Pile scanning, automatic path planning, anti-sway, target-zone control, collision avoidance and hopper interlocks can reduce manual exposure and support repeatable material flow.

    Mechanical Protection

    Overload protection, motion limits, service and emergency braking, buffers, rail sweeps, anti-derailment measures and maintenance isolators are defined for the selected design.

    Operator and Process Interface

    Cabin, radio remote or control-room operation is selected from visibility and exposure. Warning systems, cameras, exclusion zones and process interlocks support the site’s operating method.

    Final safety functions, performance levels and environmental protection are established through the approved risk assessment, site classification and destination requirements.

    Henan Mine Crane unmanned grab overhead crane in an industrial bulk material handling project
    Verified automation reference for high-dust bulk handling: unmanned grab crane with scanning, positioning and process-system integration.

    Verified Intelligent Bulk-Handling Reference

    Unmanned Grab Crane for Rotary-Kiln and Furnace Projects

    Henan Mine Crane records unmanned grab-crane deployment for Baowu Group’s Shaoguan Steel Plant 250,000-ton rotary-kiln project and Ningbo Steel’s No. 2 blast-furnace renovation, together with exports to Georgia and Vietnam. The system combines pile scanning, automatic positioning, obstacle detection, variable-frequency motion and plant-control interfaces for bulk-material work.

    These verified references are from steel-industry bulk handling, not cement production. Their relevance to a cement plant is the proven automation architecture for dusty stockpiles, remote operation and repeatable feeding. Cement service requires a new design around the specified limestone, clinker, gypsum, slag, coal or alternative fuel, its hopper arrangement and the plant’s safety classification.

    Project capacities, speeds and positioning criteria are therefore not transferred without a material study, cycle calculation and interface review.

    View Verified Project

    Engineering Deliverables and Quality Records

    A procurement-ready proposal should define the crane, process interfaces and every supply boundary that affects performance, cost or acceptance. Henan Mine Crane can align the document package with the agreed design code, inspection plan and customer responsibilities.

    Design Definition

    General arrangement, hook or grab coverage, wheel loads, clearances, cycle calculation, power demand, control philosophy and process interfaces.

    Manufacturing Control

    Material traceability, dimensional inspection, welding procedures and non-destructive examination records can be included as required by the contract.

    Testing and Handover

    Factory tests, control simulations, electrical records, installation instructions, site tests, manuals, training and critical-spares recommendations.

    Henan Mine Crane publishes its production and testing capabilities. The inspection and documentation matrix should be agreed before manufacturing so technical and commercial acceptance remain aligned.

    Installation, Commissioning and Maintenance Planning

    Plant and Civil Readiness

    Confirm runway alignment, rails, foundations, wheel-load capacity, building clearances, power, earthing, access, erection zone and shutdown interfaces before delivery.

    Functional Acceptance

    Define no-load and load tests, grab cycles, throughput demonstration, automation modes, interlocks, communication interfaces and operator training in the contract.

    Lifecycle Availability

    Plan inspection of ropes, grabs, sheaves, brakes, wheels, rails, gearboxes, motors and electrical systems around production and shutdown schedules; stock critical spares before handover.

    For an operating cement plant, delivery and erection must be coordinated with process availability, dust-control systems and planned shutdown windows. For a new plant, crane wheel loads, clearances, maintenance openings, power demand and data interfaces should be frozen before structural design is completed.

    Cement Plant Crane Price and Supply Scope

    September 2026 public-market pricing supports preliminary equipment-only budgets of approximately US$5,000–US$60,000 for many light or medium maintenance cranes, US$15,000–US$120,000+ for conventional double-girder process and maintenance cranes, and US$10,000–US$95,000+ for conventional grab overhead cranes. These broad bands overlap because capacity alone does not define a crane.

    Automated A6–A8 grab systems, large spans, high throughput, redundant controls, pile scanning, dust-classified equipment or multi-crane coordination can exceed the conventional bands and require an engineered quotation. The figures are market-planning values, not a Henan Mine Crane offer, and normally do not represent a complete installed cement-plant system.

    Commercial package Items to define before price comparison
    Crane equipment Bridge or gantry structure, trolley or hoist, drives, electrics, controls, access and safety devices
    Handling and automation package Grab, hook block, lifting beam, scanning, anti-sway, positioning, cameras, communications and process interfaces
    Runway and civil interface Rails, supporting steel, foundations, conductor system, embedded parts, access platforms and structural checks
    Environmental compliance Dust protection, hazardous-area certification, thermal measures, coatings, ventilation and documentation
    Logistics and installation Packing, inland transport, ocean freight, insurance, unloading, erection, supervision and shutdown work
    Testing and support Test loads or material trials, third-party inspection, commissioning, training, spares and warranty boundary

    A valid supplier comparison requires the same capacity, span, lifting height, duty, material and grab data, control scope, environmental protection, design code, delivery term and site responsibilities. Currency, Incoterm, quotation validity, inclusions and exclusions should be stated explicitly.

    Cement Plant Crane RFQ Information

    Submit the process area and required task; handled material, loose bulk density, particle size, moisture and abrasion; required tonnes per hour; maximum maintenance load including rigging; bay, pile, bunker and hopper drawings; span, travel length and lifting height; operating cycles; temperature, dust and hazardous-area data; runway or foundation information; power supply; control and DCS/MES interfaces; destination and applicable code; project schedule; and required freight, installation, testing, training and spare-parts scope.

    Send Project Requirements
    A defined crane configuration, interface schedule and itemized commercial scope can then be prepared.

    Frequently Asked Questions

    What type of crane is used in a cement plant?

    Grab overhead cranes serve defined bulk-material stores and feed points. Single- or double-girder hook cranes serve kiln, crusher, mill, cooler, fan and workshop maintenance. Gantry cranes can cover outdoor equipment or laydown yards.

    How is grab-crane capacity calculated?

    Crane capacity must cover the grab self-weight plus the material payload. Payload and grab volume are checked from bulk density, fill factor, particle characteristics and the required operating cycle.

    Can one crane handle limestone, clinker, gypsum and coal?

    Only after each material is evaluated. Density, abrasion, moisture, particle size, flow behavior, contamination limits and hazardous-area classification may require different grabs, operating modes or separate equipment.

    Does every cement plant crane need explosion protection?

    No. Explosion protection is required only where the plant has defined a hazardous gas or combustible-dust area. Coal, petcoke or alternative-fuel zones must be checked against the site’s formal classification.

    What crane duty class is suitable for cement service?

    Duty follows actual cycles and load spectrum. Occasional maintenance may use a lighter class, while continuous grab handling generally requires a higher-duty design. The class must be calculated rather than selected from the industry name.

    Can a cement grab crane operate automatically?

    Yes. Options include pile scanning, automatic target selection, path planning, anti-sway, collision avoidance, hopper interlocks and DCS or MES communication. Functional boundaries and manual fallback modes must be defined.

    What protection is required near a kiln or clinker cooler?

    Protection depends on measured ambient and radiant heat. The design may require shielding, high-temperature components, ventilation, cooling, derating, protected cables and an inspection plan suited to thermal cycling.

    Can an existing cement-plant runway be reused?

    Reuse is possible only after the rails, beams, columns, connections, alignment and allowable reactions are verified for the new crane wheel loads, duty, braking forces and local requirements.

    How much does a cement plant crane cost?

    Preliminary equipment-only market bands extend from about US$5,000 for simple maintenance cranes to US$120,000+ for conventional larger systems. Automated grab, hazardous-area and plantwide packages require a project quotation.

    What information is needed for a cement crane quotation?

    Provide the task, material data, throughput, maintenance-load schedule, layout, span, height, travel length, cycles, environment, area classification, runway data, power, controls, destination, code and required supply scope.

    Technical content record

    Prepared by Henan Mine Crane Technical Sales · Technically reviewed by Crane Engineering · Last reviewed September 2026

    Related Cement Plant Crane Products

    Henan Mine Crane intelligent grab overhead crane for cement bulk material handling

    Intelligent Grab Overhead Crane

    High-duty four-rope grab system with optional automated bulk-material control.

    View Details →

    Henan Mine Crane grab and hook dual-purpose overhead crane for mixed cement plant duties

    Grab-and-Hook Overhead Crane

    Dual-purpose crane for defined bulk handling and conventional hook lifting.

    View Details →

    Henan Mine Crane double-girder overhead crane for cement mill and kiln maintenance

    Double-Girder Overhead Crane

    Hook crane for heavier process-equipment maintenance and controlled positioning.

    View Details →

    Henan Mine Crane explosion-proof bridge crane for classified cement plant fuel areas

    Explosion-Proof Bridge Crane

    Project-matched lifting equipment for documented hazardous gas or dust zones.

    View Details →

    Henan Mine Crane double-girder gantry crane for cement plant outdoor service yards

    Double-Girder Gantry Crane

    Rail-mounted outdoor crane for equipment yards and shutdown support areas.

    View Details →

    Cement Plant Lifting Proposal

    Request a Cement Plant Crane Quote

    Share the process duty, material and throughput data, maintenance loads, plant layout, required coverage, operating cycle, environment, area classification, destination and delivery boundary. Henan Mine Crane will develop a defined crane configuration and commercial proposal for the cement operation.

    Henan Mine CraneDiscuss your requirements ↗
  • Ceiling Crane Systems for Workshops and Warehouses

    Ceiling Crane Systems for Workshops and Warehouses

    Ceiling Crane Systems for Workshops and Warehouses

    Henan Mine Crane · Building-Supported Lifting Systems

    Ceiling Crane Systems for Workshops and Warehouses

    Ceiling-supported and overhead crane configurations engineered around building strength, usable hook height, floor clearance, load coverage, duty cycle and installation scope.

    Henan Mine Crane configures single-girder underhung cranes, multi-point suspension cranes, multi-support double-girder systems and conventional top-running bridge cranes. The correct arrangement depends on the structural load path, required capacity, span, headroom, operating frequency and production layout.

    Henan Mine Crane ceiling suspended overhead crane in a large industrial workshop
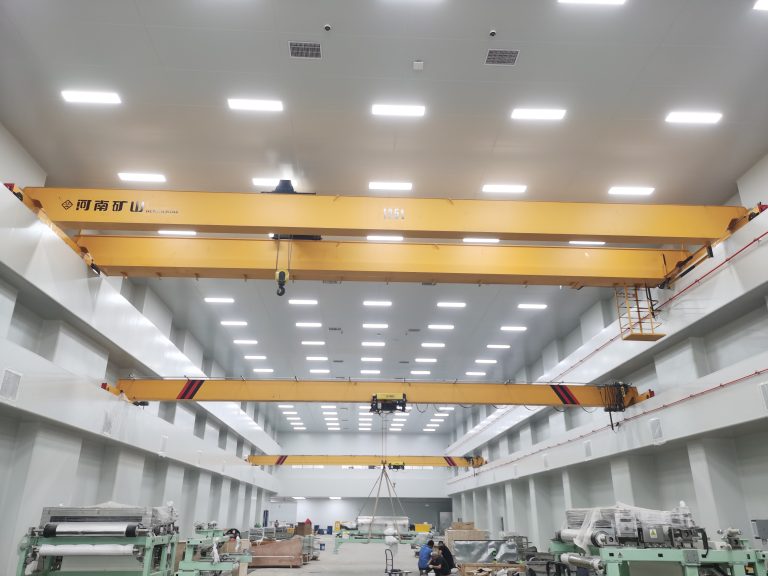
    A ceiling crane uses an engineered runway and building support system to keep production floors clear while providing defined lifting coverage.

    SUPPORT OPTIONS

    Roof, Runway or Columns

    CRANE OPTIONS

    Underhung & Top Running

    COVERAGE OPTIONS

    Bridge, Monorail & Workstation

    QUOTE BASIS

    Crane + Building Interface

    What Is a Ceiling Crane?

    A ceiling crane is a commercial search term for lifting equipment installed above a work area and supported by the building structure or a dedicated overhead runway. In industrial projects, the term normally refers to an underhung bridge crane, ceiling-mounted workstation crane, suspended monorail or conventional overhead bridge crane. It does not describe one fixed crane model.

    An underhung crane travels on the lower flange of runway beams suspended from structural roof members or engineered supports. This arrangement avoids runway columns on the production floor and can improve bridge and hoist end approach. It is often selected for manufacturing cells, warehouses, maintenance bays and buildings where clear aisles are essential.

    A top-running bridge crane travels on rails above runway beams. It generally provides a stronger route for higher capacities, wider spans and more demanding duties, but the runway may require building columns or an independent support structure. A ceiling-mounted workstation system uses lighter enclosed or rolled tracks for ergonomic handling and localized coverage. A monorail follows a fixed path rather than covering a rectangular bay.

    The architectural ceiling finish is not a structural support. Crane loads must transfer through approved runway beams, hangers, roof trusses, columns or an independent frame. Structural capacity, connection details, dynamic forces and existing-building condition require verification before fabrication or installation.

    Ceiling Crane Configurations

    01 · Single-Girder Underhung Crane

    A compact bridge suspended below two runways. Electric wire-rope or chain hoists provide three-axis load movement while preserving floor access and useful side approach.

    02 · Low-Headroom Underhung Crane

    A compact hoist and optimized girder connection increase usable hook height where roof clearance is limited. Rail elevation, beam depth and hook dimension require coordinated checking.

    03 · Multi-Point Suspension Crane

    Three or more runway support lines distribute loads across a wider building area and extend coverage for long-span or multi-bay workshops. Support synchronization and alignment are central design requirements.

    04 · Multi-Support Double-Girder Crane

    A suspended double-girder arrangement provides greater rigidity, higher capacity potential and a stable platform for large-span assembly, maintenance and aircraft-hangar applications.

    05 · Top-Running Bridge Crane

    The bridge runs above runway rails and transfers loads through runway beams and columns. This configuration is normally considered when capacity, span, duty or trolley requirements exceed a practical suspended arrangement.

    06 · Workstation Crane or Monorail

    Light-duty workstation bridges cover defined cells, while monorails move loads along a fixed route. Both can reduce manual handling when full-bay industrial crane coverage is unnecessary.

    Compare Ceiling Crane Systems

    System Support Arrangement Capacity Position Coverage and Application Primary Engineering Check
    Single-girder underhung crane Two suspended runway beams Light to medium industrial lifting Rectangular bay with strong side and end approach Roof reactions, bottom-flange capacity, span and hanger spacing
    Multi-point suspension crane Three or more suspended support lines Medium-duty and extended coverage Long workshops, multiple process zones and retrofit layouts Load sharing, support tolerances, synchronized travel and rail alignment
    Multi-support double-girder underhung crane Multiple roof-supported runways Higher capacity and large-span engineered projects Hangars, large assembly buildings and equipment maintenance Building load map, girder rigidity, wheel reactions and installation sequence
    Top-running bridge crane Runway beams on columns or building supports Medium to heavy capacity and demanding duty Production bays requiring robust open-winch or top-running trolley systems Column reactions, rail elevation, headroom, lateral forces and foundations
    Ceiling-mounted workstation crane Roof or freestanding light-track support Light ergonomic material handling Assembly cells, packaging, machining and repetitive local lifts Load limit, track length, suspension spacing and manual or powered motion
    Suspended monorail Single overhead track route Point-to-point or process-path lifting Production lines, paint systems, maintenance routes and transfer stations Route geometry, switches, curves, support spacing and transfer points

    Selection principle: choose the support and runway arrangement before choosing the hoist. Capacity, span and hook height are not valid until the building load path and required coverage have been confirmed.

    Ceiling Crane Applications and Working Conditions

    Facility Area Typical Loads Crane Direction Procurement Objective Critical Input
    Machining and fabrication Raw material, fixtures, workpieces and machine components Single-girder underhung or top-running bridge crane Clear machine access, controlled placement and efficient bay coverage Machine positions, heaviest lift, cycle rate and hook approach
    Assembly and production cells Subassemblies, tools, jigs and production equipment Workstation bridge, underhung bridge or monorail Floor clearance and repeatable movement between stations Cell layout, travel route, handling frequency and positioning requirement
    Warehouse and logistics Palletized goods, dies, equipment and long materials Underhung bridge or multi-point suspension crane Clear aisles, rack access and broad storage coverage Rack height, truck route, stack layout and collision zones
    Maintenance and MRO bay Motors, gearboxes, pumps and machine modules Underhung service crane or monorail Occasional lifting with precise access above installed equipment Removal path, rigging height, shutdown window and service-class basis
    Aircraft hangar and large assembly Aircraft components, tooling and maintenance loads Multi-support double-girder underhung crane Large clear floor area and wide coverage without interior runway columns Hangar structure, door clearance, component geometry and multi-crane interaction
    Hazardous or controlled environment Process equipment and approved production loads Special underhung crane with project-specific protection Space utilization while meeting environmental and area requirements Hazard classification, cleanliness, corrosion, temperature and certification boundary

    Environmental protection must be selected from the actual operating area. A dust-resistant enclosure does not establish explosion protection, and a general industrial ceiling crane should not enter a classified hazardous area without a complete project-specific design and compliance review.

    Technical Selection and Specification Framework

    A ceiling crane quotation should be based on a dimensioned building and operating specification. A rated capacity alone cannot define runway reactions, usable lift, mechanism duty or the installation boundary.

    Specification Item Project Input Required Engineering Output Procurement Control
    Rated capacity Maximum lifted item plus hook block, lifting beam, clamp, magnet, C-hook, sling and every suspended component Net load and gross suspended load stated separately Future loads included only when defined and approved
    Span and runway geometry Runway rail centers, travel length, support spacing, cantilever length, curves or switches Dimensioned plan with bridge and hoist approaches Building width is not substituted for crane span
    Lift and headroom Lowest pickup, highest placement, rail elevation, roof obstructions and attachment depth Vertical section showing hook path and maintenance removal Usable hook height is checked with the actual hoist and load
    Building and runway capacity Roof truss, rafter, beam, column, connection, foundation and existing-condition data Vertical, lateral and longitudinal reactions for every support Structural approval precedes attachment fabrication
    Duty and load spectrum Moves per hour, average load, full-load frequency, shifts, annual hours and travel distance Crane and mechanism classification Production and maintenance service are evaluated separately
    Motion and positioning Hoist, trolley and bridge speeds, low-speed range, stopping distance and accuracy Drive, brake, encoder and control description Speed is balanced with stability and operating visibility
    Power and controls Voltage, frequency, phase, conductor route, isolation, pendant, radio, cabin or automation Electrical load, schematic basis and control narrative Voltage and control standard are fixed before component release
    Environment Indoor temperature, dust, humidity, corrosion, washdown, clean area or hazardous classification Protection and material schedule Environmental claims follow the complete assembly, not one component
    Safety and compliance Destination jurisdiction, governing standards, statutory registration and inspection authority Safety matrix, inspection plan and document register Certification scope and third-party involvement are agreed in the contract
    Installation and acceptance Site access, lifting equipment, work permits, power readiness, test weights and production shutdown Method statement, commissioning procedure and handover plan Labor, runway work and load testing are included or excluded explicitly

    Published Henan Mine Crane configuration ranges: European-style single-girder suspended cranes are offered at 1–10 t, 7.5–28.5 m span and 6–20 m lift; multi-point suspension cranes at 1–20 t, 10–60 m span and 6–18 m lift; multi-support double-girder underhung cranes at 3–40 t, 10–80 m span and 6–30 m lift. Every final parameter remains project-specific.

    Safety, Controls and Compliance

    Safety begins with the building interface because every suspended runway reaction enters the roof or structural frame. Mechanical, electrical and operational protection is then selected from crane type, load, duty, environment and governing jurisdiction.

    Structural Load Path

    Runway beams, hangers, connections, trusses, columns and foundations require defined reactions, approved materials and traceable installation details.

    Hoisting Protection

    Overload limitation, upper and lower limits, emergency stop, brake control, rope or chain guidance and hook-latch requirements follow the selected hoist and service.

    Bridge and Trolley Retention

    End stops, buffers, wheel engagement, anti-drop or anti-derailment provisions and controlled travel address suspended running equipment.

    Travel and Collision Control

    End limits, warning devices, restricted zones and anti-collision functions protect multiple cranes, walls, equipment and maintenance areas.

    Electrical Protection

    Isolation, short-circuit and overload protection, protective grounding, control voltage, conductor guarding and enclosure selection support safe operation and servicing.

    Operator Visibility

    Pendant travel, radio control, lighting, alarms and camera options are arranged around load path, aisle traffic and blind areas.

    Inspection Access

    Platforms, access points, lockout locations and component removal clearances are coordinated with roof members and adjacent utilities.

    Standards Basis

    ASME B30.17 covers cranes and monorails with underhung trolley or bridge; top-running arrangements may invoke ASME B30.2 or another governing standard. Local law remains controlling.

    Building Integration, Headroom and Hook Coverage

    The word “ceiling” describes location rather than structural capacity. Finished ceiling panels, purlins and secondary framing should not be treated as crane supports unless the project structural design specifically assigns that function. Loads must reach engineered roof trusses, rafters, primary beams, columns or an independent support frame.

    A suspended runway introduces vertical wheel loads, dynamic effects, bridge acceleration and braking forces, skew forces and local connection reactions. Multi-point cranes also require controlled load distribution across several runway lines. Building analysis should evaluate the governing crane positions and simultaneous crane combinations.

    Headroom must be calculated from rail elevation through the end truck, bridge girder, hoist body, hook block, rigging and load. Underhung systems often improve side and end approach, while a low-headroom hoist can increase usable lift. Actual geometry matters more than a generic “low headroom” label.

    For an existing facility, survey data should include structural drawings, field dimensions, member condition, previous alterations, roof services and allowable connection methods. Reinforcement, dedicated runway steel or a freestanding system may provide a safer commercial route when the existing roof cannot accept crane reactions.

    multi-support ceiling crane with underhung bridge and roof-supported runways
    Runway spacing, hanger locations, roof reactions and hook coverage must be coordinated as one building-and-crane system.

    Application Case: Large-Span Aircraft Assembly and Maintenance Hangar

    large-span suspended ceiling crane configuration for aircraft hangar operations
    A multi-support suspended bridge can cover a wide hangar while preserving clear floor routes for aircraft, platforms and maintenance equipment.

    Henan Mine Crane documents a multi-support double-girder underhung configuration for aircraft manufacturing plants, maintenance hangars and large assembly workshops. The published product family covers 3–40 t capacity, 10–80 m span, 6–30 m lifting height and A3–A5 working classes, with project-specific power and control arrangements.

    The application challenge is a broad lifting area with minimal ground obstruction, substantial component dimensions and multiple pickup positions. Several ceiling-supported runway lines distribute the bridge reactions across the approved building structure, while the double-girder bridge provides rigidity for long-span movement and controlled positioning.

    A project package should include the hangar structural model, runway-reaction schedule, door and roof clearances, lifting zones, aircraft and tooling envelopes, permitted crane combinations, control philosophy, inspection access and phased installation method. Published ranges identify engineering capability but do not replace project calculations or structural approval.

    View Multi-Support Ceiling Crane →

    Engineering, Manufacturing and Quality Documentation

    A ceiling crane package must connect approved building data to structural design, runway fabrication, mechanisms, electrification, inspection and site acceptance. Required records should be listed before manufacturing release.

    automated crane girder welding workstation at Henan Mine Crane
    Approved drawings, controlled fabrication, dimensional inspection and functional testing support traceable ceiling-crane delivery.

    Design Package

    General arrangement, support layout, runway reactions, hook approaches, mechanism class, electrical demand and control narrative.

    Structural Records

    Material identification, welding procedures, welder qualifications, dimensions, runway connections and specified examination records.

    Mechanism Data

    Hoist, motor, gearbox, brake, rope or chain, wheel, bearing, buffer and lubrication information matched to declared duty.

    Electrical Documents

    Single-line diagram, schematics, drive data, protection settings, conductor details, control voltage and configured parameters.

    Inspection and Tests

    Inspection plan, witness points, dimensions, drives, brakes, limits, alarms, interlocks and contracted load testing.

    Handover Package

    Final drawings, support schedule, test records, manuals, spare-parts list, maintenance schedule and commissioning data.

    Installation, Commissioning and Lifecycle Planning

    Building Survey and Approval

    Verify drawings, member sizes, support locations, connection restrictions, roof services, access and existing structural condition before final design.

    Runway and Hanger Fabrication

    Manufacture runway beams, hangers, brackets and connections from approved details with traceable materials, dimensions and inspection points.

    Installation Method

    Plan delivery sequence, work-at-height controls, lifting equipment, temporary support, assembly zones and production shutdown requirements.

    Rail and Runway Alignment

    Check elevation, straightness, span, support spacing, flange condition, end stops and transitions before bridge installation and powered travel.

    Electrification

    Install conductors, festoons, isolators, grounding, control stations and communication equipment with protected access for inspection.

    Functional Commissioning

    Verify drives, brakes, limits, buffers, warning devices, anti-collision, radio or pendant control and emergency functions without load.

    Load and Site Acceptance

    Complete required proof, rated-load and operational tests under the approved procedure with documented results and assigned responsibilities.

    Preventive Maintenance

    Establish inspection intervals for supports, connections, rails, end trucks, wheels, brakes, ropes or chains, conductors and controls from actual service.

    Ceiling Crane Price and Project Cost

    Ceiling crane pricing depends on more than bridge capacity. Runway beams, hangers, roof reinforcement, electrification, access, installation and acceptance can materially change total project cost. The published North American bridge-crane figures below provide general market budget context only; they are not fixed Henan Mine Crane prices.

    Budget Level Indicative Market Position Typical Scope Main Cost Drivers Commercial Control
    1 t ceiling-hung monorail benchmark Around US$15,000 Approximately 25 ft of track under the published regional conditions Track length, support steel, lift, power, installation and access Confirm whether building connections and testing are included
    1–2 t workstation crane benchmark Around US$30,000–40,000 A 1 t, 20 × 25 ft example at about US$30,000; a 2 t example at about US$40,000 Coverage, support method, bridge quantity, hoist and installation Freestanding support can increase the published example by roughly 30%
    5 t single-girder bridge benchmark Around US$40,000 General crane near or below a 40 ft span under stated regional conditions Span, lift, duty, runway, electrification and installation Underhung supports and roof work require separate confirmation
    10 t single-girder installed benchmark Around US$65,000 Conventional general-duty bridge crane with installation in the published example Building interface, controls, labor, access, testing and region Not a fixed ceiling-suspended system price
    5 t double-girder installed benchmark Around US$60,000 Conventional double-girder bridge under the stated market conditions Trolley type, headroom, span, runway and installation Building reinforcement and special controls may be additional
    10 t double-girder installed benchmark Around US$100,000 General double-girder system under the stated market conditions Duty, speed, controls, runway, access and regional labor Not directly comparable with a large-span multi-support crane
    Single-girder underhung ceiling crane Project quotation Bridge, hoist, end trucks, suspended runways, conductors and documents Roof reactions, hanger spacing, hook approach, support steel and freight Crane supply and building work are separated
    Multi-point or multi-support ceiling crane Project quotation Multiple runway lines, synchronized travel, engineered controls and site services Capacity, span, support count, alignment, building analysis and commissioning Evaluate total installed scope rather than bridge equipment alone

    Commercial normalization: compare crane equipment, hoist, runway steel, hangers, building reinforcement, electrification, controls, documentation, packing, freight, erection, commissioning, load testing, training and spare parts as separate line items.

    Information Required for a Ceiling Crane Quote

    A technically comparable quotation requires building information and operating data together. Dimensioned plans, roof or structural drawings, load sketches and site photographs should accompany the following information.

    Load Data

    Maximum and typical mass, dimensions, center of gravity, pickup points, rigging or attachment weight and any future lifting requirement.

    Coverage and Geometry

    Required travel area, runway length, span, rail elevation, lowest pickup, highest placement, hook approach and overhead obstructions.

    Building Structure

    Roof truss, rafter, beam, column and foundation drawings; support spacing; allowable reactions; connection restrictions and structural condition.

    Duty and Throughput

    Moves per hour, load spectrum, shifts, annual operating hours, full-load frequency, travel distance and production consequence.

    Motion and Control

    Required hoist, trolley and bridge speeds, low-speed range, pendant or radio control, cabin, automation and positioning tolerance.

    Power and Environment

    Voltage, frequency, phase, indoor temperature, dust, humidity, corrosion, washdown, clean-area or hazardous classification.

    Installation Conditions

    Site access, delivery opening, available lifting equipment, work-at-height rules, shutdown window, power readiness and test weights.

    Commercial Boundary

    Trade term, runway and support steel, reinforcement, installation, statutory inspection, training, spare parts, documentation language and schedule.

    Ceiling Crane FAQ

    Is a ceiling crane the same as an overhead crane?

    Ceiling crane is a broad commercial term. It can describe an underhung bridge, suspended monorail, workstation crane or conventional overhead bridge crane installed near the roof. The support arrangement determines the correct technical name.

    Can a crane be attached directly to a building roof?

    Only approved structural members and connections may carry crane loads. Finished ceiling panels and unverified secondary members are not crane supports. A qualified structural assessment is required before installation.

    What is the difference between underhung and top-running cranes?

    An underhung bridge runs below suspended runway beams and preserves floor space. A top-running bridge runs above runway rails and generally provides a stronger route for higher capacities, wider spans or heavier duty.

    What capacity is practical for an underhung ceiling crane?

    Many conventional underhung systems are applied at 10 t or below, although engineered multi-point and double-girder systems can cover higher capacities. Building reactions, span and duty determine practical limits.

    Does an underhung crane improve hook coverage?

    Underhung end trucks and cantilever options can improve bridge end approach, and the hoist may travel closer to runway limits. Final coverage depends on end-truck length, girder connection, hoist geometry and structural clearances.

    Can a ceiling crane be installed in an existing workshop?

    Yes, subject to survey and structural verification. Reinforcement, dedicated runway steel or an independent support frame may be necessary when existing roof members or connections cannot accept crane reactions.

    Which data controls usable lifting height?

    Rail elevation, end-truck depth, bridge girder depth, hoist headroom, hook block, rigging, attachment and load height jointly define usable lift. Roof height alone is insufficient.

    How much does a ceiling crane cost?

    Total cost depends on capacity, span, duty, runway, hangers, reinforcement, power, controls, freight, installation and testing. General bridge benchmarks support early budgeting, while a ceiling-supported system requires a project quotation.

    Which safety standard applies to an underhung crane?

    ASME B30.17 addresses cranes and monorails with an underhung trolley or bridge in applicable projects. Other jurisdictions may require EN, ISO, national or statutory rules. The governing basis must be stated in the contract.

    What should be included in the final quotation?

    The proposal should identify crane and hoist parameters, runway and support scope, reactions, controls, safety devices, documents, tests, packing, freight, erection, commissioning, training, spare parts, exclusions and schedule.

    Request a Ceiling Crane Proposal

    Submit the load list, building drawings, required coverage, capacity, span, lifting height, duty, support information, power supply, operating environment, installation boundary and destination. Henan Mine Crane will prepare a coordinated technical configuration and commercial quotation.

    Henan Mine CraneDiscuss your requirements ↗
  • Bulk Handling Cranes

    Bulk Handling Cranes

    Bulk Handling Cranes

    Henan Mine Crane · Engineered Bulk Material Handling Systems

    Bulk Handling Cranes

    Bulk handling cranes provide repeatable loading, transfer, stockpiling and discharge of coal, ore, coke, slag, sand, aggregates, biomass, waste and other loose materials. Henan Mine Crane configures grab overhead cranes, grab gantry cranes, automated grab systems and portal harbor cranes around material properties, required throughput, operating duty and site layout.

    A dependable specification requires more than crane capacity and grab volume. Bulk density, particle size, moisture, flow characteristics, abrasion, pick-and-discharge geometry, cycle time, grab self-weight, environmental protection and project supply scope determine system performance and commercial cost.

    intelligent double girder grab crane for high duty bulk material handling
    A double-girder grab crane combines high-duty lifting machinery, a material-specific grab and process controls for repeated bulk transfer.

    SYSTEM FAMILY

    Overhead, Gantry or Portal

    PRIMARY ATTACHMENT

    Mechanical or Powered Grab

    OUTPUT BASIS

    Net Payload and Actual Cycle

    PRICE BASIS

    Project-Specific Quotation

    What Are Bulk Handling Cranes?

    Bulk handling cranes are crane systems equipped with a grab bucket or another process attachment for repeated handling of unpackaged loose material. The search term describes an application family rather than one fixed crane model. The correct system may be an overhead crane above a bunker, a gantry crane over an open stockyard, an automated grab crane serving a production process or a portal crane transferring cargo between vessel and quay.

    The crane, grab and supporting infrastructure operate as one material-handling system. A quotation based only on nominal tonnage can produce insufficient net payload, slow cycle performance, premature wear or an incomplete supply scope. Material, throughput, duty, geometry, control, environment and commercial boundaries must be defined together.

    Production Feeding

    Transfer from storage pits or stockpiles into hoppers, furnaces, crushers, mixers and process lines.

    Stockyard Transfer

    Loading, unloading, sorting and stockpile management across indoor or outdoor storage areas.

    Waste and Recycling

    High-cycle movement, blending and feeding of municipal, industrial or recyclable material.

    Port Cargo Handling

    Ship-to-shore or terminal transfer where outreach, luffing, slewing and grab duty are required.

    Selection Considerations

    01 / MATERIAL

    Material Characteristics

    Bulk density, particle range, moisture, flowability, compaction, abrasion, corrosion and temperature determine the grab.

    02 / PAYLOAD

    Capacity and Grab Weight

    The specification must state whether capacity means total suspended mass or net material capacity below the grab.

    03 / OUTPUT

    Throughput and Cycle

    Required tonnes per hour, pick and discharge points, travel distances and operating availability establish performance.

    04 / GEOMETRY

    Pickup and Discharge Layout

    Stockpile, pit, bunker, vessel and hopper geometry determine span, lift, travel, outreach and clearance.

    05 / CONFIGURATION

    Overhead, Gantry or Portal

    Coverage, supporting structure, outdoor exposure, floor traffic and vessel interface govern the system type.

    06 / DUTY

    Service and Reliability

    Cycles per hour, operating hours, load spectrum, starts and production criticality establish the required duty.

    07 / ENVIRONMENT

    Dust, Corrosion and Hazard

    Airborne dust, combustible material, corrosion, humidity, wind, rain and classified areas require formal review.

    08 / SCOPE

    Controls and Project Boundary

    Cabin, radio or automation plus rails, power, civil work, freight, erection, testing and training must be defined.

    A complete enquiry includes material data, required throughput, pickup-and-discharge arrangement, capacity basis, span, lifting height, travel length, operating duty, control method, power supply, environment, installation country and supply boundary.

    Bulk Handling Crane System Comparison

    The product ranges below support initial configuration screening. Final capacity, span, lifting height, duty, grab and standards remain project-specific.

    Crane System Published Product Range Suitable Application Selection Boundary
    Single-Girder Grab Overhead Crane 1–10 t · 7.5–28.5 m span · 6–30 m lift · A3–A5 Intermittent light- or medium-duty transfer in warehouses and process areas Economical where throughput and net payload suit the single-girder design
    Intelligent Double-Girder Grab Crane 5–50 t · 10.5–31.5 m span · 6–30 m lift · A6–A8 High-cycle coal, ore, coke, slag, lime, sand and aggregate handling Demanding duty, high output, process integration or automated operation
    Grab and Hook Overhead Crane 5–16 t · 10.5–31.5 m span · 6–20 m lift · A5–A6 Facilities handling loose material and conventional unit loads in one bay Attachment conversion and capacity definition require coordination
    Grab and Hook Gantry Crane 1–20 t · 6–30 m span · 4–18 m lift · A5 Outdoor yards or buildings without a suitable elevated runway Rails, foundations, wind, power supply and traffic routes govern scope
    Portal Harbor Crane Project-specific capacity, radius and duty Bulk cargo transfer between vessel, quay hopper, truck and terminal storage Vessel, quay, outreach, grab duty, wind and marine protection are essential

    Material Data and Grab Bucket Selection

    single girder grab crane handling loose bulk material
    Grab geometry and crane capacity are coordinated so the loaded bucket remains within the permissible suspended load.

    Four-Rope Mechanical Grab

    A four-rope clamshell grab uses dedicated holding and closing ropes and is commonly selected for repeated high-cycle handling of free-flowing material. Winches, drums, ropes and grab are engineered together.

    Electro-Hydraulic or Motor Grab

    A powered grab supports detachable or mixed-use duties. Attachment power, cable management, maintenance access and achievable cycle performance require inclusion in the crane design.

    Orange-Peel or Special Grab

    Irregular scrap, rock and mixed waste may require an orange-peel or purpose-designed attachment. Tine shape, penetration, closing force and retention are matched to the feed.

    Grab and Hook Combination

    A detachable grab and hook configuration supports mixed bulk and unit-load work. Conversion frequency, connection method and attachment storage form part of the specification.

    Net Material Payload

    Material per cycle = effective grab volume × bulk density × practical fill factor.

    Grab volume alone does not establish output. The loaded grab, ropes and rigging must remain within the stated capacity basis. Contract documents should explicitly distinguish total suspended mass from net material capacity below the grab.

    Material Principal Conditions Selection Priorities
    Coal and biomass Low or variable density; dust and combustible-material risks may apply Bucket volume, dust control and ignition-hazard assessment
    Ore, coke and slag High density, abrasion, impact and possible elevated temperature Grab strength, wear protection, mechanism duty and temperature suitability
    Sand and aggregates Flowable but abrasive; moisture changes filling and release Shell closure, cutting edges, fill factor and hopper opening
    Waste and recyclables Irregular shapes, variable density, entanglement and uncertain composition Attachment penetration, retention, fire monitoring and protected controls
    Grain and feed Dust, hygiene, contamination and moisture considerations Tight-closing grab, cleanable surfaces and dust-hazard engineering
    Cement and fine powder High dust and leakage potential during closing, travel and discharge Enclosed grab and extraction assessment; conveyor or pneumatic transfer may be preferable

    Throughput, Cycle Time and Duty

    Bulk crane output depends on material retained in each grab cycle and the number of complete cycles achieved under operating conditions. Rated crane capacity is not equivalent to hourly throughput.

    STEP 1

    Material per Cycle

    Effective grab volume, bulk density and realistic fill factor establish net material mass. Grab and rigging mass are checked against capacity.

    STEP 2

    Complete Cycle Time

    Closing, hoisting, trolley and bridge travel, lowering, opening, return travel and positioning form the complete cycle.

    STEP 3

    Operating Availability

    Pile shape, digging resistance, hopper waiting, spillage, control response, inspection and process delays reduce practical output.

    Theoretical hourly throughput = net material per cycle × completed cycles per hour.

    Guaranteed process output requires agreed material properties, operating route, availability assumptions and acceptance-test conditions. Duty classification is selected from load spectrum and cycle demand, not nominal capacity alone.

    Overhead and Gantry Configurations

    grab and hook dual purpose overhead crane for bulk and unit loads
    A dual-purpose overhead crane supports bulk and hook lifting when attachment conversion, capacity and duty are correctly defined.

    Grab Overhead Crane

    An overhead crane provides full-bay coverage without crane legs occupying the floor. It is suitable above storage pits, bunkers and process buildings with an adequate runway structure.

    Single- or Double-Girder Design

    Single-girder construction can suit moderate capacity and intermittent service. Double-girder construction is evaluated for higher duty, larger grabs, wider spans, open-winch machinery and maintenance access.

    Dedicated or Dual-Purpose

    A dedicated grab crane supports repeated process duty. A grab-and-hook crane covers more task types but requires defined conversion procedures and may not match a dedicated high-cycle system.

    Control Method

    Cabin operation supports process supervision; radio control supports selected manual duties; automated operation supports repeatable routes and plant integration.

    Grab Gantry Crane

    A gantry crane transfers reactions through crane legs to rails and foundations. It can cover outdoor stockpiles or buildings without an elevated overhead-crane runway.

    Rails and Foundations

    Wheel loads, rail alignment, foundation stiffness, drainage and settlement criteria affect reliable travel. Vehicle and pedestrian crossings require coordinated protection.

    Outdoor Protection

    Wind limits, storm anchoring, rail clamps, corrosion protection, rain covers, drainage and cable management form part of an outdoor design.

    grab gantry crane with forged travel wheels for bulk stockyard handling
    Grab gantry crane engineering includes the crane, rails, wheel loads, outdoor protection and safe stockyard interfaces.

    Portal Cranes for Bulk Cargo Terminals

    portal harbor crane configured for bulk cargo handling at a marine terminal
    Portal crane selection combines vessel geometry, quay conditions, working radius, grab duty and terminal logistics.

    Vessel and Quay Interface

    Working radius, vessel hatch position, water-level range, quay elevation and portal clearance establish the operating envelope.

    Luffing, Slewing and Travel

    Coordinated hoisting, luffing, slewing and portal travel determine cargo cycle time. Drives and controls reflect duty, wind and terminal procedures.

    Quay Infrastructure

    Rail gauge, wheel loads, power, storm anchoring, cable routes, access and maintenance zones must suit the quay structure.

    Cargo Route

    Grab discharge may feed a hopper, conveyor, truck or storage system. Dust containment, spillage control and traffic coordination affect the terminal solution.

    Bulk Handling Crane Specification Schedule

    Item Required Project Data Engineering Significance
    Material Name, density, particle size, moisture, temperature, abrasion, corrosion and hazard data Governs grab type, volume, materials, wear protection and environment package
    Throughput Required t/h, peak demand, operating hours, availability and acceptance basis Establishes payload, speed, cycle model, crane quantity and duty
    Capacity basis Total suspended load or net capacity under grab; grab and rigging mass Prevents ambiguity in usable material payload and structural load
    Geometry Span, lift, travel, outreach, pile, pit, bunker, vessel and hopper dimensions Defines crane arrangement, grab path and cycle distance
    Duty and speeds Cycles, load spectrum, starts, hoisting, trolley and crane travel requirements Aligns structures, motors, brakes and controls with service demand
    Control Cabin, radio, automation, position data, anti-sway and plant interfaces Defines sensors, PLC architecture and operating functions
    Power and environment Voltage, frequency, temperature, dust, wind, rain, humidity and classified zones Sets electrical design, enclosures, coating and special protection
    Project boundary Crane, grab, rails, runway, power, civil work, freight, erection, testing, training and spares Enables technically and commercially comparable quotations

    Controls, Automation and Environmental Protection

    Motion and Position

    Variable-frequency drives, position feedback and anti-sway functions can support controlled cycles and accurate discharge.

    Automatic Routes

    Defined pick, transfer and discharge paths can include pile scanning, restricted zones and hopper selection.

    Dust and Wear

    Controlled discharge, protected enclosures, suitable coating and replaceable grab wear parts reflect the material and atmosphere.

    Hazardous Areas

    Zone classification, ignition data, equipment category, surface temperature, earthing and all ignition sources require formal review.

    Automatic-cycle boundaries, sensor inputs, interlocks, recovery modes, manual override, data interfaces, output assumptions and site-acceptance conditions should be defined before contract award. A single protected component does not make the complete crane suitable for a hazardous area.

    Bulk Handling Crane Project Case

    unmanned grab bucket overhead crane in a steel plant bulk material process
    An unmanned grab bucket crane supports repeatable material transfer in a steel-production environment.

    STEEL INDUSTRY · AUTOMATED BULK TRANSFER

    Unmanned Grab Bucket Overhead Crane for Baowu Group Shaoguan Steel Plant

    The project serves a bulk-material process associated with rotary-hearth-furnace steelmaking. Crane configuration and automatic control were developed for repeated material pickup, transfer and discharge within the designated production area.

    Process Requirement

    Repeatable material movement, defined operating zones and coordinated discharge into the production process.

    Engineering Focus

    Grab logic, crane positioning, automatic routes, operational interlocks and plant-system coordination.

    Procurement Relevance

    The installation demonstrates why crane machinery, grab, automation and process interfaces must be treated as one system.

    Engineering, Manufacturing and Documentation

    ENGINEERING

    Application Review

    Material, output, cycle, capacity, geometry, duty, wheel loads, controls and site interfaces are reviewed before design.

    MANUFACTURING

    Controlled Production

    Fabrication, machining, assembly, coating and component installation follow approved drawings and agreed processes.

    VERIFICATION

    Inspection and Testing

    Dimensions, welds, mechanisms, electrics, protection devices and factory functions are checked under the contract plan.

    DOCUMENTATION

    Project Document Package

    Approved drawings, data sheets, electrical diagrams, manuals, certificates, inspection records and test documents are supplied as specified.

    Installation, Commissioning and Maintenance

    Pre-Installation Verification

    Runway or rail geometry, foundations, clearances, power, access, lifting plan, storage area and responsibilities are confirmed before erection.

    Commissioning and Acceptance

    Alignment, electrical checks, limits, brakes, protective functions, load tests, grab operation and process interfaces follow the agreed plan.

    Duty-Based Maintenance

    Ropes, drums, sheaves, brakes, wheels, rails, grab pins, bushes, shells, cutting edges, hydraulics and electrics require documented inspection.

    Lifecycle Planning

    Commissioning and operating spares should reflect crane criticality and local availability. Grab and rope-system wear parts deserve particular attention in abrasive or continuous-duty service.

    Bulk Handling Crane Price

    Bulk handling crane price varies substantially because capacity, grab system, duty, span, lift, cycle performance, automation and supply boundary differ between projects. Equipment-only figures cannot be compared directly with installed systems including runway or rails, power, civil work, freight, erection and commissioning.

    Market budget indications place 10 ton grab overhead crane equipment across approximately USD 5,000–95,000. Detailed 10 ton double-girder grab crane examples appear around USD 27,000–59,000. General 16–20 ton gantry crane examples are approximately USD 25,000–80,000 before normalizing grab, duty, rail, foundation, electrical and site scope. Automated grab cranes and portal harbor cranes require engineered project quotations. These figures are not Henan Mine Crane quotations.

    Crane Equipment

    Structure, trolley, drives, ropes, drums, brakes, wheels, electrics, controls and safety functions.

    Grab and Process

    Grab type, volume, wear materials, attachment power, automation, sensors and process interfaces.

    Infrastructure

    Runways, columns, rails, foundations, power, cable routes, dust control and access platforms.

    Delivery and Site Work

    Packing, freight, import charges, erection, commissioning, tests, training and spares.

    Information Required for an Accurate Price

    Material and density · particle size and moisture · required t/h · pickup and discharge geometry · capacity basis · grab type · span and lift · travel or outreach · duty and cycles · control and automation · dust, corrosion and hazard conditions · power · rails and civil scope · installation country · delivery terms · erection, testing, training and documentation.

    Bulk Handling Crane FAQ

    What materials can a bulk handling crane move?

    Typical applications include coal, ore, coke, slag, lime, sand, aggregates, biomass, waste and selected grain products. Material data determine suitability.

    Which grab is suitable for bulk material?

    Free-flowing material commonly uses a clamshell grab. Irregular scrap or waste may require an orange-peel or special-purpose grab. Geometry, force, wear and power arrangements are material-specific.

    Does crane capacity include the grab?

    Capacity terminology must be stated in the contract. It may describe total suspended mass including the grab or net material capacity below the grab.

    How is throughput calculated?

    Net material per cycle comes from effective grab volume, density and fill factor. Hourly output then depends on the complete operating cycle and availability.

    When is a gantry crane preferable?

    A gantry crane is commonly evaluated for outdoor yards or sites without an elevated runway. Coverage, foundations, traffic and environmental exposure govern the choice.

    Can bulk handling cranes operate automatically?

    Automation can include position feedback, pile scanning, anti-sway, defined routes, hopper selection, restricted zones and plant-control communication.

    Can a grab crane handle combustible dust?

    Suitability depends on formal hazard classification. The complete crane, grab, electrical system, mechanical ignition risks, earthing and dust controls must comply.

    Is a grab crane suitable for fine powder?

    An enclosed grab and extraction can be evaluated, but conveyor, screw or pneumatic transfer may be more suitable where containment and continuous flow govern.

    How much does a bulk handling crane cost?

    Price depends on capacity, grab, duty, output, span, automation, infrastructure, protection, freight and site services. Supply boundaries must be normalized before comparison.

    What is required for a quotation?

    Material, throughput, layout, capacity basis, span, lift, travel, duty, controls, environment, power, infrastructure, country and required project scope are required.

    Application Engineering and Commercial Proposal

    Request a Bulk Handling Crane Quote

    Submit material properties, required throughput, pickup and discharge layout, capacity basis, span, lifting height, duty, controls, environment, power, installation location and project scope. Henan Mine Crane will prepare a crane configuration and commercial quotation from verified application data.

    Henan Mine CraneDiscuss your requirements ↗
  • Bridge Crane

    Bridge Crane

    Bridge Crane

    Henan Mine Crane · Industrial Lifting Systems

    Bridge Crane

    Move materials across your production bay with a bridge crane configured for the load, building and work cycle. Henan Mine Crane manufactures single-girder, double-girder and underhung bridge cranes for workshop production, warehouse handling, equipment assembly and maintenance.

    From a compact electric-hoist arrangement to a dedicated process crane, the proposal brings together rated capacity, hook coverage, runway loads, lifting speeds and controls. Send your lifting requirement and building drawing to discuss a suitable configuration.

    Double-girder electric-hoist bridge crane from Henan Mine Crane
    Double-girder electric-hoist arrangement. Final capacity, span and lifting height are specified for each project.

    BRIDGE STRUCTURE

    Single or Double Girder

    RUNWAY ARRANGEMENT

    Top Running or Underhung

    LIFTING SYSTEM

    Hoist or Winch Trolley

    PROJECT INPUTS

    Load, Span, Lift and Duty

    Bridge Crane Design and Applications

    A bridge crane carries a hoist or trolley across a bridge spanning the working bay. The bridge travels along elevated runways, while the hoist raises and lowers the load. Together, these movements serve material pickup, transfer and placement points within the available hook coverage.

    In industrial enquiries, bridge crane and overhead crane usually describe this same moving-bridge arrangement. An electrically powered travelling design is also called an EOT crane. Its suitability depends on the layout and handling task, rather than which name appears in the enquiry.

    Workshop and Assembly

    Transfer components between machining, fabrication and assembly stations. Define the load orientation and positioning needs at each station.

    Warehouse and Maintenance

    Serve storage lanes and equipment repair areas within the crane bay. Check hook access around racks, machines, doors and overhead services.

    Process Material Handling

    Match the lifting attachment and operating duty to bulk materials, steel products or specialised production tasks.

    Bridge Crane Technical Specifications

    A bridge crane is a configurable system. The technical proposal should identify the selected values and interfaces below; one general parameter range cannot describe every single-girder, underhung and process crane.

    Parameter Project Specification
    Rated lifting capacity Specified for the maximum lifted load and the agreed treatment of slings, lifting beams, grabs or other attachments.
    Crane span Set from the runway centreline spacing. Provide support positions for an underhung or multi-support system.
    Lifting height and hook levels State the highest and lowest required hook positions, including any pit or below-floor lift.
    Runway length and hook coverage Define longitudinal travel and hook approaches at the sides and ends of the bay.
    Bridge and hoist arrangement Single or double girder; electric hoist or winch trolley; top-running or underhung bridge as applicable.
    Crane and mechanism duty Selected from load spectrum, operating cycles and service requirements under the agreed design standard.
    Hoisting and travel speeds Matched to handling time, load behaviour and placement accuracy. Speed control is specified for each motion.
    Control method Pendant, radio remote, cabin or project-specific automation, with a defined control priority.
    Electrical supply Confirm site voltage, frequency, phases, earthing system and the incoming power connection.
    Environment and protection Specify ambient conditions, outdoor exposure, dust, corrosion, heat and any hazardous-area classification.
    Runway reactions and interfaces Confirm crane weight, wheel loads, wheel spacing, rail or beam interface and support reactions in the technical proposal.

    For a metric 5-ton lifting requirement, explore the 5 Ton Overhead Crane page. A higher capacity or a different duty cycle should be assessed with the same building and load information.

    Selection Considerations

    01 / LOAD

    Load and Handling Route

    List the heaviest load, typical load, dimensions, centre of gravity and lifting attachment. Mark pickup and placement points so the hook can reach each position without obstruction.

    02 / BUILDING

    Building and Runway

    Provide a plan and cross-section showing runway levels, roof steelwork, columns and services. Existing supports require a structural assessment using the proposed crane reactions.

    03 / OPERATION

    Production Cycle

    Describe lifts per hour, travel distances, operating shifts and the proportion of lifts near rated load. These inputs affect mechanism selection and duty classification.

    04 / SITE

    Environment and Access

    Identify heat, dust, moisture, corrosion or explosive atmospheres. Reserve access for inspection, lubrication and removal of components during maintenance.

    Single-girder and double-girder describe the bridge beams. Top-running and underhung describe how the bridge travels on its runways. A hoist suspended below a single girder does not, by itself, make the whole crane an underhung crane.

    Bridge Crane Compared with Other Industrial Crane Configurations

    Compare the complete arrangement at the required load and hook position. Structural weight, available headroom and support costs depend on the proposed design; neither girder count nor rated capacity alone determines the lowest installed cost.

    Configuration Structural Arrangement Application Fit Selection Trade-Off
    Single-Girder Bridge Crane One bridge girder, commonly with an electric hoist travelling below it. General workshop, warehouse and maintenance handling. Compare hook height, side approaches, hoist duty and runway loading for the actual layout.
    Double-Girder Bridge Crane Two bridge girders supporting the selected trolley and lifting mechanism. Projects needing a different trolley layout, lifting envelope or equipment arrangement. A double girder does not automatically mean heavy duty; confirm the rated duty and complete crane dimensions.
    Underhung Bridge Crane Bridge end carriages travel on the lower flanges of suitable runway beams. Layouts where a suspended runway arrangement suits the building. Assess runway beam flanges, connections, support capacity and clearance. Roof suitability is project-specific.
    Multi-Support Underhung Crane An underhung bridge arranged across multiple runway supports. Large assembly areas and facilities with an engineered multi-rail layout. Coordinate support spacing, alignment and load distribution across the supporting structure.
    Gantry Crane A bridge supported by travelling legs, with the runway typically at ground level. Yards or buildings where an elevated runway is unsuitable. Allow for legs, ground rails or travel lanes, foundations and operating clearances.

    Hoist, Trolley and Bridge Movement

    Hoisting: Vertical Movement

    The lifting mechanism raises and lowers the suspended load. Select rope travel, hook arrangement, braking and speed control around the lift and placement requirements.

    Trolley Travel: Across the Bay

    The trolley or travelling hoist moves along the bridge. Trolley dimensions and end clearances affect how closely the hook can approach either side.

    Bridge Travel: Along the Bay

    End carriages move the bridge along the runways. Wheel arrangement, drive selection and runway alignment must work together over the travel length.

    For restricted headroom, compare the proposed highest hook level and crane envelope on the building cross-section. A low-headroom hoist or a different bridge arrangement may help, but the result must include roof clearance, services and maintenance access.

    Single-girder bridge crane with electric hoist from Henan Mine Crane
    Single-girder bridge arrangement with an electric hoist for general material handling.
    Multi-support double-girder underhung bridge crane from Henan Mine Crane
    Multi-support underhung arrangement for a building designed around the suspended crane loads.

    Load Handling and Special Environments

    The lifting attachment and process can change the crane specification as much as the load capacity. Discuss these configurations when a general hook crane does not cover the work:

    • Double-trolley handling: for long components or work requiring two lifting points. Define individual hoist ratings, shared-load limits, hook spacing and the intended coordinated movements.
    • Grab bridge cranes: for bulk materials. Provide bulk density, material condition, discharge height and required throughput so grab capacity and duty can be evaluated together.
    • Electromagnetic bridge cranes: for suitable steel products. Identify material shape, surface condition and temperature, and define the required response to a loss of lifting power.
    • Metallurgical bridge cranes: for specified hot-material or production duties. Describe the process, radiant heat and consequences of interrupted lifting; molten-metal handling requires a dedicated design review.
    • Explosion-proof bridge cranes: for a defined hazardous area. Supply the site classification and gas or dust information so equipment protection and required documentation can be assessed.

    Safety, Controls and Redundancy

    The safety and control schedule should be part of the quotation. Required protections and optional functions must be clearly identified for the chosen crane and site.

    Load and Motion Protection

    Specify overload protection, hoisting and travel limits, braking arrangements, emergency stops and relevant electrical protections. Confirm how each function will be demonstrated at acceptance.

    Operator Control

    Choose pendant, radio remote or cabin operation around visibility and operator access. For multiple control stations, define selection priority and the response to a lost command signal.

    Shared Runways and Automation

    Where cranes share a bay, assess collision prevention and operating separation. Anti-sway, positioning and process interfaces require a defined performance target and acceptance method.

    Dual hoists, additional brakes, monitoring and standby functions are engineered for the intended duty. Their availability and scope should be confirmed in the technical proposal rather than assumed from the crane name.

    Installation, Acceptance and Maintenance

    Installation Interfaces

    Agree who supplies the crane, runway beams, rails, conductors, supporting steelwork and foundations. Provide unloading access, assembly space and the planned installation window.

    Acceptance and Documentation

    Agree drawing approvals, inspection records, electrical diagrams, manuals and the factory and site test scope before ordering. Define the responsibilities for site commissioning and operator familiarisation.

    Maintenance Access

    Plan access to the hoist, trolley, wheels, drives and power supply. Identify replacement clearances and the spare parts needed for the operating schedule.

    For a replacement bridge crane, survey the existing runway and electrical supply. The previous crane’s rated capacity alone does not establish compatibility: the new crane may have different wheel loads, wheel spacing, dimensions or power demand.

    What Determines Bridge Crane Price?

    Bridge crane price depends on rated capacity, span, lifting height, duty, hoist arrangement and operating environment. Runway equipment, installation work, controls, testing and delivery scope can also change the total project cost.

    When comparing bridge cranes for sale, request quotations against the same specification. Ask each supplier to identify the crane supply, runway and power supply scope, selected components, drawings, inspections, delivery terms and installation responsibilities.

    Equipment

    Bridge, end carriages, hoist or trolley and controls.

    Site Interfaces

    Runway, electrical feed, supports and installation scope.

    Project Delivery

    Documentation, testing, packing, transport and commissioning.

    Bridge Crane FAQ

    Is a bridge crane the same as an overhead crane?

    In normal industrial usage, the terms often refer to the same crane with a moving bridge on elevated runways. EOT describes an electrically powered overhead travelling crane. Confirm the structure and operating requirements in the specification.

    Should I choose a single-girder or double-girder bridge crane?

    Compare the proposed hook coverage, headroom, runway reactions, duty and total installed scope. Both arrangements can serve industrial handling, and the right choice depends on the specific layout and work cycle.

    Does an underhung crane require a suitable roof structure?

    An underhung crane requires suitable runway beams and supports, which may connect to a building structure or a separate engineered support system. The supporting structure and connections must be assessed for the crane loads.

    Can a bridge crane be fitted to my existing runway?

    Possibly. Provide the runway drawings and survey information, existing crane data, rail or beam details and power supply. Compatibility must be checked against the new crane’s dimensions, wheel arrangement and reactions.

    Can two hoists lift one load together?

    A coordinated lifting arrangement can be engineered for that duty. Individual hoist capacities do not by themselves establish the permissible combined load. Define load sharing, lifting points, motion control and fault response in the proposal.

    Can the same bridge crane work outdoors or in a hazardous area?

    These conditions need a suitable design. Outdoor projects require assessment of exposure and wind-related requirements; hazardous areas require equipment matched to the site classification. State the environment at the enquiry stage.

    What information is needed for a bridge crane quotation?

    Send the maximum and typical loads, attachment details, span, lifting height, runway length, building drawing, work cycle, power supply and project location. Include any inspection, documentation or installation requirements.

    Request A Bridge Crane Quote

    Send Henan Mine Crane your lifting requirement and building layout for a project-specific bridge crane proposal. Include the following details to help define the configuration and scope:

    • Maximum load, typical load and lifting attachment
    • Span, required hook levels and runway length
    • Operating cycle, site environment and electrical supply
    • Project country, drawings, delivery needs and installation scope
    Henan Mine CraneDiscuss your requirements ↗
  • Bridge Crane for Sale

    Bridge Crane for Sale

    Bridge Crane for Sale

    Henan Mine Crane · New Industrial Lifting Equipment

    Bridge Crane for Sale

    Henan Mine Crane manufactures new bridge cranes for production workshops, warehouses, maintenance bays, steel plants, power facilities and process industries. Each crane is configured around the lifted load, span, lifting height, operating duty, building clearances and working environment.

    Available systems include single-girder, double-girder, top-running, underhung, electric-hoist, winch-trolley and special-purpose bridge cranes. Supply can cover crane equipment, runway interfaces, electrification, project documentation, delivery and agreed installation services.

    New single girder bridge crane for sale from Henan Mine Crane
    New bridge crane equipment configured for the required load, building geometry and operating cycle.

    EQUIPMENT CONDITION

    New · Project Configured

    BRIDGE STRUCTURE

    Single or Double Girder

    RUNWAY ARRANGEMENT

    Top Running or Underhung

    CONTROL OPTIONS

    Pendant · Radio · Cabin · Automation

    New Bridge Cranes for Industrial Facilities

    A bridge crane provides three-axis material movement within a defined bay. The bridge travels along parallel runways, the hoist or trolley moves across the bridge, and the lifting mechanism raises or lowers the load. This arrangement keeps the operating floor clear while providing controlled lifting coverage over production and storage areas.

    Bridge crane, overhead crane and EOT crane are common commercial terms for this equipment family. The purchase specification must identify the actual bridge structure, runway arrangement, hoisting mechanism, duty and control system rather than relying on the product name alone.

    Supply position: The offered range covers newly manufactured, project-configured bridge cranes. Used equipment, rental cranes and generic component kits are outside the standard product scope.

    Bridge Crane Applications

    Manufacturing and Assembly

    Machinery components, fabrications, tooling, molds and assemblies moving between production stations.

    Warehousing and Maintenance

    Inbound materials, stored equipment, maintenance assemblies and controlled loading operations.

    Steel and Metallurgy

    Coils, plates, billets, ladles, scrap, process equipment and high-temperature production materials.

    Power and Process Industry

    Generators, turbines, pumps, production equipment and planned maintenance loads.

    Bulk Material Handling

    Grab-crane systems for coal, ore, aggregate, biomass, waste and process feedstock.

    Hazardous and Special Areas

    Classified, corrosive, dusty, high-temperature or cleanliness-controlled operating environments.

    Bridge Crane Specifications

    The final crane schedule is developed from the operating requirement and building interface. Approved values are stated in the technical proposal and general arrangement drawing.

    Specification Available Engineering Direction Required Project Information
    Rated Capacity Configured for the selected crane model and service Maximum suspended load, attachment weight and load spectrum
    Span and Runway Length Matched to the working bay and runway geometry Runway gauge, travel distance, support spacing and rail data
    Lifting Height Project-defined hook travel and approach dimensions Lowest pickup, highest placement, rigging height and building clearances
    Working Class Selected from operating time, cycles and load spectrum Lifts per hour, shifts, loaded cycles, travel distance and process criticality
    Hoisting Mechanism Wire-rope electric hoist, winch trolley or special mechanism Capacity, duty, lift, speed, headroom, redundancy and access
    Control Method Pendant, radio remote, cabin, remote station or automated control Visibility, travel distance, staffing, speed control and process interfaces
    Power Supply Electrical equipment matched to the destination supply Voltage, frequency, phases, earthing and site distribution
    Operating Environment General, outdoor, hazardous, corrosive, dusty or high-temperature configuration Temperature, humidity, contaminants, hazard classification and local requirements

    Selection Considerations

    01 / LOAD

    Maximum Load and Attachment

    Rated capacity includes the lifted item and below-the-hook equipment. Load geometry and centre of gravity affect the handling arrangement.

    02 / COVERAGE

    Working Area and Hook Envelope

    Span, runway length, hook approaches, lift and obstructions determine usable coverage inside the crane bay.

    03 / DUTY

    Load Spectrum and Operating Cycle

    Working class and mechanism ratings are aligned with operating hours, starts, travel and the proportion of heavy lifts.

    04 / BUILDING

    Runway and Structural Capacity

    Wheel loads, lateral forces, rail size, support spacing and allowable clearances must be coordinated with the supporting structure.

    05 / OPERATION

    Control and Motion Performance

    Control position, speeds, variable-frequency drives, anti-sway and positioning functions are selected for the handling process.

    06 / PROJECT SCOPE

    Delivery and Site Responsibility

    Runway, power distribution, freight, erection, commissioning, testing and documentation require defined responsibility.

    Bridge Crane Compared with Other Industrial Crane Configurations

    Equipment selection is based on building support, required lifting coverage, operating duty and load-handling method. The same rated capacity can require a different configuration when the site or production process changes.

    Configuration Structural Arrangement Application Position Critical Selection Inputs
    Single-Girder Bridge Crane One bridge girder with an under-running hoist General workshop, warehouse, assembly and maintenance lifting Capacity, span, headroom, duty and runway reactions
    Double-Girder Bridge Crane Two bridge girders with a selected hoist or trolley Heavier loads, demanding duty, wider spans and process service Load spectrum, trolley arrangement, hook envelope and access
    Underhung Bridge Crane Bridge travels beneath compatible suspended runways Facilities where elevated top-running runway columns are unsuitable Roof structure, runway flange, support spacing and clearances
    Double-Trolley Bridge Crane Two lifting mechanisms operating on one bridge Long loads, two-point handling and defined coordinated operations Individual capacities, combined load, hook spacing and control logic
    Gantry Crane Leg-supported bridge travelling on ground-level rails or wheels Outdoor yards or facilities without suitable elevated runway support Ground conditions, foundations, travel lanes, wind and cantilevers

    Bridge Crane Configurations

    The commercial description “bridge crane for sale” covers several structural and mechanical arrangements. Configuration selection affects hook coverage, building loads, maintenance access, operating performance and total project scope.

    Single girder electric hoist bridge crane configuration

    Single-Girder Bridge Crane

    A single bridge girder carries an electric wire-rope hoist operating beneath the girder. This arrangement is widely specified for general manufacturing, warehousing, maintenance and assembly service.

    • Compact bridge structure for general industrial lifting
    • Electric-hoist mechanism with pendant or radio control
    • Selection governed by span, headroom, duty and runway capacity
    Double girder electric hoist bridge crane configuration

    Double-Girder Bridge Crane

    Two bridge girders support an electric hoist or winch trolley. The layout permits alternative hook approaches, service platforms and mechanism arrangements for demanding production service.

    • Suitable for higher loads, wider spans or intensive duty
    • Electric-hoist or open-winch trolley configurations
    • Access platforms and process equipment available by specification
    Underhung bridge crane operating beneath suspended runways

    Underhung Bridge Crane

    The bridge end trucks travel beneath suspended runway beams. This structure can provide lifting coverage where floor-supported runway columns are restricted or where the building has a compatible supporting system.

    • Suspended runway arrangement for defined building conditions
    • Roof and runway support require structural confirmation
    • End approaches and suspension points established by layout
    Explosion-proof bridge crane for a classified industrial environment

    Special-Purpose Bridge Crane

    Hazardous, metallurgical, high-temperature, corrosive and bulk-handling applications require equipment developed for the stated operating conditions rather than a general-purpose crane with isolated component changes.

    • Hazard classification and material properties defined at enquiry stage
    • Special mechanisms, protection, controls and lifting attachments
    • Technical scope aligned with project acceptance requirements

    Crane, Runway and Building Integration

    A bridge crane is part of an integrated load path. Crane wheel reactions pass through the rails and runway beams into building columns, freestanding supports or another approved structure. The complete arrangement must accommodate vertical loads, transverse forces, longitudinal forces, operating clearances and maintenance access.

    New-Build Facility

    Early coordination permits the crane envelope, runway elevation, support spacing, electrical feed and maintenance access to be incorporated into the building design.

    Existing Runway

    An existing runway requires dimensional and structural assessment. Rail condition, alignment, span, support spacing and permissible reactions are evaluated against the proposed crane.

    Freestanding Runway

    Independent runway columns can separate crane reactions from the main building where space, foundations and operating routes permit a freestanding support structure.

    Interface control: Crane span, rail level, runway gauge, wheel loads, end approaches and power-feed location are recorded in approved project drawings. Building and runway suitability remain subject to competent structural verification.

    Hoisting, Travel and Control Systems

    Hoisting Mechanism

    Wire-rope electric hoists provide a compact mechanism for many general-purpose single- and double-girder cranes. Winch trolleys permit alternative reeving, machinery layouts, access provisions and redundancy for demanding service. The selected mechanism is matched to capacity, lift, speed, duty, headroom and maintenance strategy.

    Bridge and Trolley Travel

    Motor, brake, wheel and drive arrangements are developed for the travel distance, acceleration, operating frequency and required positioning performance. Variable-frequency control can provide smoother acceleration and deceleration where the process requires controlled motion.

    Control Options

    • Pendant control: local control for conventional workshop service.
    • Radio remote control: flexible operating position with the specified control functions.
    • Operator cabin: elevated control position for process cranes, long travel routes or defined visibility requirements.
    • Remote station: control from a fixed operating room or protected station.
    • Automated operation: positioning, interlocks and process communication developed from a defined functional specification.

    Safety and Environmental Configuration

    Protective functions are selected for the crane duty, motion hazards, load characteristics, access conditions and applicable project requirements. The final safety schedule forms part of the technical agreement.

    Load and Hoist Protection

    Upper and lower travel limits, overload protection, braking and other mechanism safeguards are specified for the lifting arrangement.

    Travel Protection

    Travel limits, end stops, buffers, audible or visual warnings and anti-collision functions are applied for the operating layout.

    Electrical Protection

    Isolation, emergency stopping, short-circuit, phase and motor protection are coordinated with the electrical design and site supply.

    Access and Maintenance

    Platforms, walkways, guards, access points and maintenance clearances are defined where required by the crane arrangement.

    Hazardous Areas

    Gas or dust classification, temperature class, zone information and material properties are required before an explosion-protected configuration can be established.

    Outdoor or Corrosive Service

    Weather exposure, wind, ambient temperature, humidity, chemicals and coating requirements determine environmental protection measures.

    Bridge Crane Supply Scope

    A commercially complete comparison requires a defined boundary between crane equipment, runway infrastructure, site services and installation activities. Henan Mine Crane prepares the proposal against the agreed project scope.

    Scope Group Typical Content Commercial Definition
    Crane Equipment Bridge structure, end carriages, hoist or trolley, travel drives, electrical equipment and controls Included equipment and technical limits stated in the proposal
    Power and Electrification Crane power feed, conductor system, festoon system, isolators and interface cabling as specified Supply termination points and site connections identified
    Runway System Rails, runway beams, columns, brackets, buffers and associated structural items when included Equipment-only, runway-inclusive or interface-data-only basis stated
    Transport and Site Services Packing, freight, unloading, erection supervision, installation, commissioning and testing Commercial terms, destination and responsibility matrix agreed
    Project Documentation Drawings, technical schedules, electrical information, manuals and agreed inspection records Document language, format, approval stages and submission schedule stated

    Bridge Crane Price Factors

    Bridge crane pricing is project-specific because capacity alone does not define the structure, mechanism, duty or installed scope. A quotation becomes commercially comparable only when all suppliers receive the same technical and delivery requirements.

    Capacity, Span and Lift

    Structural size, hoisting equipment, rope capacity and building interface change with the lifting geometry.

    Duty and Motion Control

    Operating cycle, speeds, variable-frequency drives, positioning functions and redundancy affect equipment selection.

    Environment and Compliance

    Hazard protection, temperature, corrosion, outdoor exposure and project documentation add specific engineering requirements.

    Runway and Site Scope

    Runway steelwork, freight, unloading, installation, commissioning and site testing can materially change total project cost.

    A structured breakdown of equipment and installed-system cost drivers is available under Overhead Crane Pricing.

    Manufacturing, Inspection and Documentation

    Bridge crane steel structures inside a Henan Mine Crane manufacturing workshop
    Crane structures and production equipment inside a Henan Mine Crane manufacturing workshop.

    Henan Mine Crane develops the manufacturing package from the approved technical agreement and general arrangement. Production and inspection requirements are connected to the selected crane structure, mechanisms, electrical system and contracted documentation scope.

    • Approved general arrangement and interface dimensions before production release
    • Material, fabrication and component controls defined by the manufacturing plan
    • Electrical and mechanism checks performed against the agreed configuration
    • Inspection points, test activities and records aligned with the contract
    • Packing and shipment planning coordinated with crane dimensions and destination

    Manufacturing facilities and production scenes are presented in the Henan Mine Crane factory display.

    Delivery, Installation and Commissioning

    01

    Engineering Approval

    Project drawings, interfaces, components and commercial scope are approved before manufacturing release.

    02

    Production and Inspection

    Manufacturing, assembly checks and agreed inspection activities follow the approved project package.

    03

    Packing and Delivery

    Shipment preparation reflects component protection, lifting points, package dimensions and the contracted delivery term.

    04

    Site Installation

    Runway readiness, lifting access, electrical services and installation responsibilities are confirmed before site work.

    05

    Commissioning and Handover

    Functional checks, agreed testing, records and operating documentation support formal project handover.

    Production and delivery timing depends on configuration, drawing approval, material and component availability, inspection scope, transport arrangement and site readiness. Contract milestones are established for the individual order.

    Information Required for a Bridge Crane Quotation

    A complete enquiry enables technical evaluation, layout development and a defined commercial scope. Building drawings, runway data and load information can be attached where available.

    Load and Operation

    • Maximum and typical lifted loads
    • Load dimensions and attachment weight
    • Lifts per hour and operating shifts
    • Required speeds and positioning needs

    Building and Coverage

    • Runway span and travel length
    • Required lifting height and hook positions
    • Runway and support information
    • Roof, wall and service clearances

    Environment and Supply

    • Indoor or outdoor operating conditions
    • Temperature, dust, corrosion or hazard data
    • Electrical power supply
    • Project location, delivery term and required services

    Bridge Crane for Sale FAQ

    What information is needed to price a bridge crane?

    Essential inputs include rated load, span, lifting height, runway length, operating duty, environment, power supply, control method, project location and required supply scope. Drawings and existing-runway data improve dimensional and structural coordination.

    Is a bridge crane the same as an overhead crane or EOT crane?

    These terms commonly describe the same family of travelling-bridge lifting equipment. The technical specification must still define the girder arrangement, runway type, lifting mechanism, duty and control system.

    When is a double-girder crane selected instead of a single-girder crane?

    A double-girder arrangement is evaluated when load, span, working duty, lifting envelope, trolley layout, maintenance access or process requirements exceed the preferred operating range of a single-girder arrangement. Selection is based on the complete project rather than capacity alone.

    Can a new bridge crane operate on an existing runway?

    Compatibility is determined from the existing rail and runway geometry, alignment, support condition and allowable reactions. The proposed crane wheel loads, wheel spacing, power demand and clearances must be assessed against the existing structure.

    Does the quoted bridge crane price include runway beams and installation?

    Inclusion depends on the stated commercial scope. Crane equipment, rails, runway steelwork, power feed, freight, erection, commissioning and testing should be identified separately when comparing proposals.

    Can bridge cranes be configured for hazardous or high-temperature areas?

    Special configurations are available when the hazard classification, temperature, material, exposure and project requirements are defined. General-purpose equipment is not substituted for a purpose-designed crane in these environments.

    Which controls are available for a bridge crane?

    Pendant, radio remote, operator cabin, fixed-station and automated controls can be evaluated. Visibility, operating route, production interface, motion precision and site rules determine the appropriate arrangement.

    How is delivery time established?

    The delivery schedule is established after configuration and scope confirmation. Drawing approval, production complexity, component availability, inspection activities, packing, transport route and site readiness affect the contracted milestones.

    Request A Bridge Crane Quote

    Submit the required capacity, span, lifting height, duty, building information, power supply, operating environment and project location. Henan Mine Crane will develop a bridge crane proposal with the applicable configuration, technical data and defined supply scope.

    Henan Mine CraneDiscuss your requirements ↗
  • Automotive Industry Crane Systems

    Automotive Industry Crane Systems

    Automotive Industry Crane Systems

    Henan Mine Crane · Press Shop, Tooling and Vehicle Production Handling

    Automotive Industry Crane Systems

    Engineered overhead, underhung, workstation and semi-gantry crane systems for stamping dies, molds, coils, fixtures, powertrain components, vehicle assembly and plant maintenance.

    Henan Mine Crane configures each automotive industry crane around the actual load family, production sequence, die-change target, attachment, placement tolerance, duty spectrum, building interface, control architecture, safety zones and contracted project scope.

    automated mold handling crane for an automotive stamping workshop
    Automotive crane selection begins with the production task: heavy die transfer, precision fixture handling, point-of-use assembly assistance or planned equipment maintenance.

    PRIMARY DUTIES

    Dies, Fixtures, Components and Maintenance

    PLANT ZONES

    Press, Body, Powertrain and Assembly

    CRANE OPTIONS

    Bridge, Underhung, Workstation or Semi-Gantry

    CONTROL LEVELS

    Manual, Assisted, Semi-Automatic or Automatic

    What Is an Automotive Industry Crane?

    An automotive industry crane is an engineered lifting system used in vehicle plants, component factories and tooling facilities. Typical duties include press-die storage and changeover, mold transfer, steel-coil receiving, body fixture handling, robot and conveyor maintenance, engine and transmission assembly, battery-pack movement, end-of-line service and general plant maintenance.

    One crane type does not serve every automotive zone. A press shop may require a process-duty double-girder die-handling crane with a dedicated gripper and automatic positioning. A body shop may require an underhung or light workstation system around robots and conveyors. A loading edge or workshop extension may be better served by a semi-gantry crane. Capacity, precision, duty and safety architecture are therefore selected by task rather than by industry name alone.

    Henan Mine Crane develops automotive lifting solutions from double-girder bridge crane, European-style single-girder crane, single-girder suspension crane and project-specific automated handling platforms.

    Automotive Plant Crane Application Map

    A plant-wide lifting study records routine production moves, maintenance lifts, emergency recovery tasks and every interface with presses, robots, conveyors, storage systems and vehicle traffic.

    1. Coil and Blank Receiving

    Unload coils, sheet packs and production materials, then transfer them to storage or blanking lines. Coil orientation, attachment choice, surface protection, aisle clearance and delivery-vehicle exclusion determine the handling concept.

    2. Press Shop and Die Store

    Retrieve matched die sets, transport them along a protected route and position them at the press or die-change cart. High load, short change windows, offset centers of gravity and controlled seating make this the most demanding automotive crane duty.

    3. Body-in-White and Welding

    Handle fixtures, welding cells, robots, framing equipment and replacement tooling. Low headroom, crowded services and restricted robot zones often favor underhung, monorail or workstation arrangements.

    4. Powertrain and E-Drive

    Move engines, transmissions, motors, housings, machining fixtures and test equipment through defined stations. Smooth variable-speed motion, ergonomic controls and application-specific fixtures protect machined surfaces and assembly interfaces.

    5. Battery and Paint Areas

    Battery-pack assembly, cell production and paint operations have different cleanliness, fire and hazardous-area conditions. The approved environmental and area-classification documents—not the process name—determine enclosure, materials and explosion-protection requirements.

    6. General Assembly and Maintenance

    Support point-of-use lifting, conveyor work, fixture exchange, line-side replenishment and maintenance shutdowns. Coverage, approach, manual handling risk, parked-load location and unobstructed production flow shape the layout.

    automotive manufacturing crane operating above workshop equipment
    The crane envelope is coordinated with presses, die racks, robots, conveyors, utilities, maintenance access and protected pedestrian routes.

    Automotive Industry Crane System Architecture

    Bridge and Runway

    Single- or double-girder, top-running or underhung architecture is selected from capacity, span, headroom, approach, building reactions, process coverage and required stiffness.

    Hoisting Machinery

    Wire-rope hoist or open-winch machinery is sized from gross load, lift, speeds, starts, load spectrum, precision, brake strategy and required production availability.

    Die or Component Attachment

    A die gripper, lifting beam, tong, C-hook, vacuum device, manipulator or certified hook rigging engages the declared load family and includes positive confirmation where the risk assessment requires it.

    Motion and Positioning

    Variable-frequency drives, controlled acceleration, creep speed, encoders, load-height feedback and anti-sway functions support stable travel and repeatable final approach.

    Controls and Plant Interface

    Pendant, radio, cabin or remote-control-room operation can integrate with press controls, WCS, MES, storage management, access gates and maintenance authorization.

    Inspection and Recovery Access

    Walkways, platforms, isolation stations, attachment stands, rescue provisions and component-removal paths are coordinated with production equipment before fabrication.

    double girder overhead crane platform for automotive tooling and maintenance
    A double-girder platform provides the structural and machinery base for heavy tooling, while the attachment and controls remain application-specific.

    Automotive Industry Crane Selection Considerations

    Rated tonnage is only one selection input. The complete load envelope, process sequence and consequence of delayed changeover define the appropriate crane.

    Load Family and Center of Gravity

    Maximum and minimum mass, dimensions, lifting points, center-of-gravity range, surface restrictions and orientation are documented for every die, fixture, component and maintenance load.

    Cycle and Availability

    Die changes per shift, travel path, storage retrieval, press occupancy, average load, starts per hour, annual operating hours and recovery strategy determine mechanism duty and redundancy.

    Placement and Approach

    Required coordinates, allowable approach, final speed, die-cart interface, rack geometry, press centerline and permissible alignment error are specified as measurable acceptance values.

    Building and Process Envelope

    Runway elevation, roof, columns, presses, racks, robots, conveyors, utilities, access doors and neighboring cranes are checked in a coordinated three-dimensional clearance model.

    Control and Data Scope

    Manual, assisted or automatic operation; die identification; task source; station handshakes; protected areas; event records; cybersecurity and manual recovery are defined before controls are priced.

    Environment and Maintenance

    Press-shop vibration, lubricants, welding fumes, dust, heat, washdown, paint solvents, dry-room conditions and scheduled shutdown windows establish the protection and service concept.

    Automotive Industry Crane Configurations Compared

    Configuration Typical Automotive Duty Principal Strength Critical Engineering Check
    Automated Die-Handling Process Crane Die store retrieval, press feeding and return Repeatable high-load transfer with dedicated attachment and plant integration Die database, grip confirmation, center of gravity, positioning, protected route and safe recovery
    Double-Girder Overhead Crane Heavy dies, molds, presses, fixtures and maintenance loads Higher capacity, stiffness and available hook height for process-duty handling Duty class, load share, wheel loads, headroom, attachment mass and final approach
    Single-Girder Low-Headroom Crane Components, tooling, line maintenance and warehouse service Compact general-purpose coverage with lower structural mass Hoist approach, building reactions, actual duty and attachment clearance
    Underhung or Workstation Crane Body fixtures, powertrain components and point-of-use assembly Flexible local coverage above crowded production floors Roof support, joint and suspension loads, ergonomic force, runway layout and end stops
    Semi-Gantry Crane Loading edge, workshop extension and localized machine service Coverage where only one side of the building can support an elevated runway Ground rail, building-side reactions, skewing, traffic separation and floor obstruction

    Automotive Press Shop and Die-Handling Crane

    Press-shop availability depends on retrieving the correct die set, engaging it safely, traveling along an authorized route and placing it at the defined interface within the production change window.

    Die Store Retrieval

    The task identifies the die, rack position, mass, center of gravity, approved engagement points and destination. Rack clearances and pickup tolerance are incorporated into the attachment and positioning design.

    Grip and Load Confirmation

    Mechanical position, locking state, contact or pin engagement and load distribution can be monitored before hoisting. A confirmed signal does not override inspection of damaged or obstructed lifting points.

    Protected Transfer

    Position tracking, height limits, anti-sway, collision supervision and protected travel corridors control the movement between storage, inspection, maintenance and press-line stations.

    Press Ready Handshake

    The press, bolster, die cart, clamps, guards and access state must establish an approved transfer condition. The responsibility for each permissive is recorded in the interface matrix.

    Precision Placement

    Creep speed, load-height feedback, anti-sway and attachment adjustment support final alignment without using press equipment, racks or guides as uncontrolled mechanical stops.

    Release and Traceability

    Release is enabled only after support, position and station state are confirmed. Task completion records die identity, source, destination, time, alarms and any manual intervention.

    automated stamping shop crane with a dedicated die handling attachment
    A dedicated attachment can reduce sling handling, but every die interface, locking state, center of gravity and abnormal recovery condition still requires verification.

    Automotive Crane Attachments and Load Interfaces

    double girder overhead crane prepared for a custom automotive tooling interface

    Die Gripper or Custom Spreader

    A powered gripper or adjustable spreader supports frequent die retrieval where interfaces can be standardized. Selection covers the complete die range, engagement geometry, adjustment axes, locking confirmation, allowable side load, collision envelope and parking stand.

    Attachment deadweight reduces available net load. The crane, attachment and die are therefore evaluated as one suspended system.

    automated automotive mold transfer crane viewed from the production floor

    Beam, Sling, Tong, Vacuum Device or Manipulator

    Four-point beams and certified slings serve defined die lifting points. C-hooks or tongs can serve coils and sheet packs. Vacuum devices can handle suitable panels or sheets, while manipulators support ergonomic component positioning.

    Each device requires a declared load range, proof test, inspection criteria and energy-loss response. Surface condition, porosity, oil, curvature and temperature are included where vacuum or magnetic principles are considered.

    Die Turning

    Turning or inversion requires an engineered turning device, two-hook arrangement or dedicated station with defined load share and control sequence. Side pulling, dragging and improvised turnover are excluded.

    Component Protection

    Replaceable non-marking contact pads, controlled clamping force, soft motion profiles and approved support geometry protect machined surfaces, painted parts and precision fixtures.

    Attachment Changeover

    A multi-purpose crane requires a safe connection method, identified services, parking stands, retained capacity, changeover time and recovery procedure for an incomplete connection.

    Capacity, Duty Class and Positioning Performance

    Gross Load and Net Capacity

    Crane rated capacity must cover the heaviest die, mold, fixture or component plus the complete below-the-hook attachment and any suspended auxiliaries. The crane manufacturer accounts for the hook block and reeving within the machinery design. Eccentric centers of gravity and uneven load share are checked separately.

    Duty from the Production Profile

    ISO, FEM or CMAA classification is derived from operating hours, starts, load spectrum, travel, reversing and production consequences. A crane lifting the maximum die only occasionally can have a different duty from a lighter crane cycling continuously on an assembly line.

    Accuracy and Repeatability

    Positioning claims define measurement point, load, speed, axis, repeatability, environmental conditions and acceptance method. Structural deflection, rope stretch, sway, attachment compliance and rack or press tolerance all influence final placement.

    Performance Data Required

    • Maximum and minimum load with attachment
    • Load dimensions, lifting points and center-of-gravity range
    • Lifts per hour, shifts, annual hours and load spectrum
    • Source, destination, travel distance and lift height
    • Changeover time and required availability
    • Final approach speed and placement tolerance
    • Abnormal recovery and retained-load strategy

    Automation, WCS and Production-Line Integration

    Task and Load Identity

    WCS, MES, barcode, RFID or operator confirmation associates the physical die or component with mass, coordinates, process status and destination. Unidentified or conflicting loads enter a controlled exception state.

    Position and Anti-Sway

    Absolute or referenced coordinates, controlled acceleration, sway reduction, load-height feedback and final approach logic support stable movement without contact-based correction.

    Press and Station Handshake

    Ready, occupied, guarded, clamped, transfer enabled, release authorized, complete and fault states are exchanged with presses, die carts, racks, gates and maintenance systems.

    Protected Areas and Collision Control

    Restricted volumes, temporary maintenance zones, crane-to-crane separation, obstacle detection and speed-limited approaches are implemented under the approved risk assessment.

    Operating Modes

    Automatic, remote, local maintenance and recovery modes have defined authority, speed limits, permissives and transition conditions. Active mode and control ownership remain unambiguous.

    Diagnostics and Recovery

    Event logs, cycles, loads, sensor states and alarms support maintenance. Recovery covers incomplete gripping, lost position, unavailable destination, failed communications and power interruption.

    fully automatic crane control platform for automotive mold handling
    An automatic crane requires validated load data, station states, safety ownership, communications behavior and a controlled manual recovery path.

    Safety Functions and Environmental Boundaries

    Suspended-Load Exclusion

    Pedestrian workstations, vehicle lanes and operator positions are kept outside the suspended-load path. Automatic operation uses controlled access and a defined safe state for zone entry.

    Attachment Permissive

    Hoisting and travel permissions can depend on verified engagement, load range and attachment configuration. Release remains inhibited until the load is supported and the destination is authorized.

    Press and Robot Interlocks

    Press motion, robot zones, die-cart travel, clamps, guards and crane movement are coordinated so that conflicting commands cannot create an uncontrolled exposure.

    Overload, Limits and Brakes

    Rated-capacity protection, normal and final motion limits, brakes, buffers, travel warnings and monitored speed zones are selected under the governing code and risk assessment.

    Paint and Solvent Areas

    Explosion-protected equipment is supplied only where the approved hazardous-area classification identifies zones, gas or vapor groups, temperature class and equipment protection requirements.

    Battery Production Boundary

    Cell manufacturing, module assembly and finished-pack handling can have different dry-room, cleanliness, chemical, dust and fire conditions. The site assessment determines the applicable crane package.

    Runway, Building and Maintainability Interfaces

    Existing Building Verification

    Reuse requires verification of rails, runway beams, roof trusses or suspension points, brackets, columns, connections, foundations, fatigue history and measured condition. Maximum and minimum wheel reactions, lateral forces and buffer loads are issued for structural review.

    Clearance and Production Coordination

    Bridge, trolley, attachment and load envelopes are checked against presses, die racks, robots, conveyors, ducts, cable trays, lighting and fire systems. Installation is planned around production shutdowns and protected line areas.

    Maintenance Strategy

    Access platforms, safe parking, isolation, inspection positions, rope and brake service, attachment maintenance and component-removal routes are defined before procurement. Critical spare strategy reflects the production consequence of downtime.

    Site Data Required

    • Building, runway and production-layout drawings
    • Rail or suspension-point survey and allowable reactions
    • Press, rack, robot, conveyor and utility envelopes
    • Attachment parking and maintenance access
    • Power, grounding and communication networks
    • Erection opening, laydown area and shutdown window
    • Environmental and hazardous-area documents
    double girder overhead crane installation requiring building and runway verification
    The crane, runway, building, process equipment, load path and maintenance access form one coordinated installation.

    Applicable Standards and Acceptance Testing

    The contract identifies the governing jurisdiction, crane design code, electrical standard and below-the-hook lifting-device rules. Common reference frameworks include ISO 4301 for classification, ISO 9927 for inspections and ISO 12480-1 for safe use; EN 13001 and EN 15011; CMAA 70 or CMAA 74 with applicable ASME B30 requirements; and ASME B30.20 with ASME BTH-1 for relevant lifting devices.

    IEC 60204-32 can govern electrical equipment for hoisting machines, while ISO 13849-1 or IEC 62061 can inform safety-related controls. IEC 60529 addresses enclosure ingress ratings and ISO 12944 can inform coating selection. ATEX, IECEx, NEC or other hazardous-location requirements apply only where the approved project classification establishes that scope. Local law and the signed specification remain controlling.

    Design Review

    Confirm load cases, classification, general arrangement, runway reactions, attachment, die range, placement performance, safety functions, interfaces and maintenance access.

    Factory Acceptance Test

    Verify assemblies, drives, brakes, limits, load protection, attachment logic, safety functions, interface simulation, operating modes, diagnostics and contracted documentation.

    Site and Production Acceptance

    Test proof loads, representative dies, all source and destination stations, cycle time, placement, interlocks, restricted zones, communications loss and manual recovery.

    Published Automotive Mould-Handling Crane Project

    Henan Mine Crane published automotive mould handling crane project
    Published project imagery shows the automated crane and dedicated tooling installed for an automotive manufacturing application.

    Automated Mould Transfer for an Automotive Stamping Workshop

    Henan Mine Crane reports delivering a customized automated mould-handling crane for a domestic automotive manufacturer. The published scope identifies automatic positioning, WCS management, area protection, obstacle avoidance, a multidirectional special spreader, anti-sway, servo positioning and three operating modes.

    The published safety functions include laser anti-collision, light-curtain area protection, image monitoring and a 3D-vision digital-twin function. The record states that the project was developed for mould transfer in an automotive stamping workshop.

    View Published Automotive Project →

    Automotive Industry Crane Price and Budget Scope

    An automotive crane cannot be priced accurately from capacity alone. Span, duty, attachment, precision, automation, runway or support structure, line interfaces, local compliance, installation and production acceptance can change the total materially. Public prices reviewed in 2026 illustrate different supply levels and are not equivalent project quotations.

    Public Market Reference Published Price Supply Level Major Scope Boundary
    5 t Bridge Crane Guide Estimate US$6,000–12,000 Derived from a published US$1,200–2,400 per tonne crane-only guide Excludes installation and site construction; no automotive attachment, duty or automation is normalized
    5 t Single-Girder Crane Kit with Hoist US$23,250 North American component kit listing Listing includes end trucks, controls, festoon and hoist; bridge steel is sourced locally, with runway and installation outside the stated kit
    15 t Cabin-Control Double-Girder Crane Listing US$55,000–90,000 Marketplace complete-crane price signal No normalized span, duty, die attachment, controls, runway, freight, installation or acceptance scope
    7.5 t Two-Cell Freestanding Motorized Bridge System US$94,750.80 Specific retail system listing, 20 ft wide by 40 ft per cell A particular support-system layout; automotive tooling, local erection, production interfaces and acceptance remain separate
    Automated Automotive Die-Handling Crane Project Project-specific RFQ Crane, attachment, automation and contracted services A valid total requires the die database, layout, duty, cycle, positioning, WCS or MES interfaces, safety scope and destination

    Primary Price Drivers

    Capacity, span and lift; duty class and speeds; die gripper or lifting device; two-hoist or turning requirement; positioning and anti-sway; automatic controls; WCS, MES and press interfaces; safety zoning; building steel; documentation and local compliance.

    Commercial Scope to Reconcile

    Runway rails and steelwork; structural reinforcement; freight, insurance, duties and taxes; erection; electrification; commissioning; test loads; representative dies; line-interface testing; training; spares; warranty and production acceptance.

    Engineering and Procurement Deliverables

    A procurement-ready offer defines measurable performance, interfaces, evidence and commercial boundaries.

    Technical Proposal

    Design basis, crane arrangement, capacities, classification, speeds, attachment, load assumptions, precision, protection package, operating modes and stated deviations.

    Interface Schedule

    Runway reactions, power, communications, press and station I/O, coordinates, safety ownership, erection needs, civil boundaries and third-party responsibilities.

    Attachment Documentation

    Rated range, deadweight, dimensions, engagement, locking logic, proof test, inspection limits, wear parts, attachment stand and representative-load acceptance plan.

    Safety and Controls

    Risk-assessment inputs, safety-function list, restricted zones, interlock matrix, network behavior, isolation, emergency states, recovery and required conformity records.

    Quality and O&M Records

    Inspection and test plan, material and welding records as specified, coating reports, component certificates, manuals, lubrication plan, training and critical spares.

    Commercial Schedule

    Price, Incoterm, milestones, packing, freight boundary, installation, commissioning, training, acceptance, warranty, exclusions, validity and optional lifecycle services.

    Automotive Industry Crane RFQ Information

    The following data supports a configuration-based technical and commercial proposal.

    Load and Attachment Data

    Load families; minimum and maximum mass; dimensions; center of gravity; lifting points; orientation; surface restrictions; photographs or drawings; proposed gripper, beam, tong, C-hook, vacuum device or rigging.

    Process and Duty Data

    Source and destination stations; changeover sequence; lifts per hour; shifts; annual hours; load spectrum; travel distance; target cycle; placement tolerance; availability and contingency.

    Site and Environment Data

    Span, lift, runway length, building and process drawings, allowable reactions, press and rack interfaces, temperature, dust, welding, paint, clean or dry-room requirements, power and destination.

    Controls and Commercial Data

    Operating modes; WCS, MES and PLC protocols; task and die identity; safety zones; governing standards; Incoterm; freight, installation, commissioning, test and documentation boundaries.

    Frequently Asked Questions

    Which crane is used in an automotive press shop?

    A process-duty double-girder overhead crane is commonly selected for heavy die storage and changeover. A dedicated die gripper, anti-sway, precision motion and press-line interfaces may be added when cycle frequency and automation justify them.

    Is one crane suitable for the entire automotive plant?

    Usually not. Press dies, body fixtures, powertrain components, assembly tasks and maintenance loads differ in mass, frequency, precision and environment. A plant-wide lifting plan assigns a suitable crane class to each zone.

    How is die-handling crane capacity determined?

    Capacity covers the heaviest die plus the complete gripper, beam or other below-the-hook device. Center of gravity, load share, acceleration, turning requirements and governing code are then applied.

    Can the crane retrieve dies automatically?

    Yes. Automatic retrieval can combine a die database, WCS tasks, position tracking, a dedicated gripper, anti-sway, protected zones and press handshakes. Safe exception handling and manual recovery remain mandatory design elements.

    Does an automotive crane need millimetre-level positioning?

    Only where the actual station and attachment require it. The purchase specification defines the measurement point, load, speed, repeatability and acceptance method rather than using an unsupported general accuracy claim.

    Are explosion-proof cranes required in paint shops?

    Only when the approved hazardous-area classification establishes the relevant zone and protection requirements. Solvent use or a paint-shop label alone does not determine the final crane certification.

    How much does an automotive industry crane cost?

    Public figures range from crane-only estimates and component kits to complete support systems. A defensible project price requires capacity, span, duty, attachment, automation, plant interfaces, building scope, destination and acceptance criteria.

    Can an existing runway be reused?

    Only after geometry, condition, fatigue history, rails, beams, columns, connections and foundations are verified against the proposed vertical, lateral, longitudinal and buffer reactions.

    Request an Automotive Industry Crane Quote

    Submit the load or die schedule, attachment concept, handling sequence, cycle and positioning requirements, span, lift, runway and plant drawings, operating environment, control level, WCS or MES interfaces, safety zones, power supply, project destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.

    Henan Mine CraneDiscuss your requirements ↗
  • Automotive Assembly Crane

    Automotive Assembly Crane

    Automotive Assembly Crane

    Henan Mine Crane · Engineered Automotive Production Lifting Systems

    Automotive Assembly Crane

    Overhead travelling, suspended and workstation crane systems for press shops, body-in-white, powertrain machining, final assembly lines and plant maintenance in automotive manufacturing plants.

    Henan Mine Crane engineers automotive assembly cranes around the takt time, load spectrum, positioning accuracy and building interface of each production area. Each proposal defines the crane, hoist and control system, runway interface, safety functions, electrical boundary, documentation, delivery and requested site services.

    automotive assembly crane with precision positioning single beam crane by Henan Mine Crane
    A precision-positioning single beam crane of the type used for accurate, repeatable lifting at automotive production stations.

    PRIMARY SYSTEM

    Assembly Line Bridge Cranes

    CAPACITY RANGE

    0.5 t – 50 t

    TYPICAL SPAN

    7.5 m – 35 m

    CONTROL OPTIONS

    Pendant, Radio, PLC & Anti-Sway

    What an Automotive Assembly Crane Has to Do

    An automotive assembly crane is a lifting system engineered to keep pace with a production line rather than simply to move a load. In a vehicle plant, the crane is part of the process: it feeds stamping presses with dies, positions body panels and fixtures in the body shop, moves engines, transmissions and axles onto machining and marriage stations, supplies parts to assembly stations alongside the line, and supports maintenance and end-of-line operations. What separates these cranes from general workshop cranes is not usually tonnage — it is cycle profile, positioning accuracy, ergonomics and integration with the surrounding production equipment.

    Assembly duty is defined by the takt time of the plant. A station that produces a vehicle every sixty seconds cannot wait on an uncontrolled crane swing or a hoist that creeps into position. Smooth stepless speed control, anti-sway behaviour, repeatable positioning and fast but gentle load handling directly determine whether the crane supports the line or bottlenecks it. At operator workstations, low operating forces and precise inching control also decide whether lifting assists the process or becomes an ergonomic and quality problem.

    Automotive plants also impose strict building constraints. Conveyor lines, skid systems, automation cells and process equipment occupy the volume under the roof, so hook coverage, headroom, rail clearances and interference with existing steelwork often eliminate crane configurations long before price is discussed. The correct approach is to match the crane family to the area of the plant and the measured duty at each lifting point.

    Henan Mine Crane supplies automotive assembly cranes as engineered packages: bridge or suspended structure, hoist and travel machinery, control and positioning systems, runway or suspension interface, safety functions and documentation — configured against the takt time, load spectrum, accuracy and building interface of the specific line.

    Where Cranes Work in an Automotive Plant

    Press and Stamping Shop

    Double girder cranes change and transfer press dies, handle coil and blank feeding equipment and support press maintenance. Die handling is slow, precise, high-value lifting where hook approach, exact load control and reliability matter more than speed.

    Body-in-White Shop

    Cranes install and exchange welding fixtures, position body panels and subframe assemblies, and serve framing stations. Coverage must work around robots and conveyor steel, and every lift position has to repeat within the fixture tolerances of the station.

    Powertrain Machining and Assembly

    Engines, transmissions, cylinder heads and crankshafts are handled between machining cells, washing and test stations. These areas combine moderate loads with high cycle counts and demand controlled, gentle set-down on machined surfaces.

    Final Assembly Line-Side Supply

    Suspended and workstation crane systems feed seats, doors, batteries, fuel tanks, dashboards and powertrain units to the stations that install them. Low headroom, ergonomic effort levels and reach into the station without intruding on the line are the defining requirements.

    Paint Shop and Utilities

    Cranes maintain dipping, drying and treatment equipment, handle skids and carriers, and support the process tanks and ovens that run continuously. Environment class, enclosure protection and maintenance access drive the specification in this area.

    Maintenance and End-of-Line Operations

    Workshop and workstation cranes support equipment repair, test bays, wheel and headlamp alignment areas and general logistics. These cranes lift infrequently but must be available on demand, since downtime in a running plant is measured in lost vehicles per hour.

    Crane Configurations for Assembly Service

    Each production area favours a different crane family. The selection below shows how the configuration follows the load, the cycle and the building — and where each option earns or loses money over the life of the line.

    For most line-side and machining loads up to 20 t, a single girder crane with an electric hoist is the most economical configuration and covers the majority of assembly applications. European-style single girder cranes raise this baseline with FEM-oriented duty design, lower dead weight, better hook approach and smoother travel — the standard choice where high cycle counts, close tolerances or restricted building capacity apply.

    Where loads grow — press dies, skid systems, powertrain modules, complete fixtures and maintenance of heavy process equipment — double girder cranes take over, adding hook height, stiff long-travel behaviour and heavy-duty hoisting machinery. Double trolley versions handle long and flexible parts such as shafts, axles, rail segments and long weldments that would overload a single hook point or distort during lifting.

    Suspended underhung systems bolt to the building roof steel instead of running on elevated runway rails, so they reach into stations at low headroom with minimal steelwork. Multi-point suspension designs cover wide or irregular bays. Intelligent hoist cranes close the loop with controlled positioning, anti-sway and operator guidance for the highest-accuracy stations.

    double girder electric hoist bridge crane for automotive powertrain and press shop lifting
    A double girder electric hoist bridge crane of the type used for die handling, powertrain modules and heavy fixture lifting in automotive plants.

    Automotive Assembly Crane Selection Considerations

    Selection begins with the production process and works outward to the crane. The parameters below establish the specification that a quotation must be built against, and the checklist that competing offers are compared on.

    01 · Load Spectrum per Station

    List every load at every lifting point with its fixture, spreader or tooling weight. The heaviest combination at the busiest station — not the average — sets the rated capacity for the whole system.

    02 · Takt Time and Cycle Profile

    Convert line takt into lifts per hour, travel distances and full-load ratio per station. These numbers set the ISO duty class of hoist, trolley and travel mechanisms — the difference between a line-speed crane and an early failure.

    03 · Positioning Accuracy and Anti-Sway

    Define the positioning tolerance at each station and the acceptable residual sway at set-down. These requirements select between standard speed control, frequency inverter control with crawl steps, and closed-loop anti-sway positioning.

    04 · Headroom and Building Interface

    Confirm clear height, roof steel capacity, existing conveyor and utility positions, and the clearance the process needs below the hook. Low buildings push the specification towards top-running, double girder or suspended configurations.

    05 · Environment and Cleanliness Class

    Paint shops, clean zones and battery areas impose dust, temperature and contamination limits on motors, brakes and controls. The enclosure and protection class is specified per area, not per building.

    06 · Control and Line Integration

    Define interlocks with conveyors, robots, skid systems and safety circuits, the control positions operators will use, and any interface to plant PLC or monitoring systems. Integration scope changes the electrical boundary of the offer.

    07 · Ergonomics at the Station

    Where operators handle loads manually, specify the permissible operating force, the reach envelope into the station and the precision of inching control. Ergonomic limits are production limits on an assembly line.

    08 · Project Boundary and Compliance

    Assign runway or suspension steel, conductor systems, installation, commissioning, load testing, spares and certification in writing before comparing offers, and state the standards the documentation must satisfy for the plant’s market.

    Automotive Assembly Crane Configurations Compared

    The most suitable configuration serves the takt time and accuracy of the station without transferring unnecessary cost into the building structure or the maintenance schedule.

    Configuration Where It Fits Best Typical Capacity Positioning Behaviour Critical Limit
    Single girder bridge crane General assembly, machining support, logistics bays 1–20 t Good with inverter control and crawl steps Hoist under the girder reduces hook height
    European-style single girder crane High-cycle assembly stations, tight-tolerance areas Up to 20 t class Smooth FEM-oriented travel, close hook approach Higher equipment price than standard single girder
    Double girder bridge crane Press shops, powertrain, skid systems, heavy fixtures 5–50 t and above Stiff travel, maximum hook height, precise heavy lifts Heavier wheel loads and higher runway demands
    Double trolley crane Long parts — shafts, axles, rails, weldments Per project, two coordinated trolleys Synchronised two-point lifting without distortion Only justified where long-part handling is routine
    Suspended underhung system Line-side supply at stations, low-headroom bays 0.5–10 t typical Light, ergonomic, direct reach into the station Loads carried by the roof steel, not a runway
    Intelligent hoist crane Highest-accuracy stations, controlled processes Model-specific Closed-loop positioning with anti-sway Premium controls must be matched to a real accuracy need

    Automotive Assembly Crane Technical Specification Framework

    Henan Mine Crane maintains several crane families applied to automotive production service. The ranges below support preliminary configuration and are not guaranteed combinations. Final capacity, span, lift, working class, speeds and wheel loads are confirmed on the approved technical schedule and general arrangement drawing.

    Product Family Published Capacity Position Published Span Position Lifting Height Position Working Class Position Primary Assembly Use
    Single girder assembly line crane 1–20 t across the family 7.5–28.5 m or project-defined 6–18 m or project-defined A3–A5 by cycle profile General assembly, machining support and logistics bays
    European-style single girder crane Up to 20 t class 7.5–28.5 m 6–18 m or customized A5–A6 for high-cycle stations Precision, high-cycle assembly with close tolerances
    Multi-point suspension crane 0.5–10 t typical Wide or irregular bays by suspension design Project-defined by roof geometry A3–A4 line-side duty Line-side supply at stations in low-headroom bays
    Double girder assembly crane 5–50 t and above 10.5–35 m 6–30 m or project-defined A5–A6 by cycle profile Press shop die handling, powertrain and skid systems
    Intelligent electric hoist crane Model-specific Model-specific Model-specific A5–A6 based on the station Controlled positioning and monitored lifting at key stations
    Double trolley electric hoist crane 5–50 t by project configuration 10.5–31.5 m or project-defined Project-defined A5–A6 Long parts such as shafts, axles and long weldments

    A capacity shown within one family does not confirm suitability at every span, lift or duty. Long spans, high cycle counts, precision requirements and integration with line controls require project-specific calculations and verification.

    Building and Runway Interface

    An automotive plant is a dense steel environment. The crane succeeds or fails at its interfaces with the building, and every one of these points has to be resolved before manufacture begins.

    Wheel Loads and Rail Seats

    Maximum and static wheel loads, with and without load, are verified against the runway beams and building columns. A crane change on an existing runway always starts with this check, not with the catalogue.

    Suspended Loads on Roof Steel

    Underhung and multi-point suspension systems hang from the building structure. The roof steel capacity, bracing positions and allowable deflection decide whether suspension is viable and how the load paths are arranged.

    Clearance to Conveyors and Automation

    Hook coverage is mapped against conveyors, skid tracks, robot cells and process tanks. The crane must reach the defined pick-up and set-down points without entering protected volumes or intruding on safety zones.

    Power Feed and Conductor Systems

    Conductor bars or festoon systems are routed along the runway with isolation, earthing and maintenance positions defined. Power feed placement affects plant electrical layout and must be fixed early in the project.

    Controls, Positioning and Line Integration

    Control selection follows the accuracy and rhythm of the station. The same crane structure can behave completely differently under pendant, radio or programmable control, and the difference shows directly in cycle time and damage rates.

    Pendant and Radio Control

    Pendant control keeps the operator at a fixed position beside the load; radio remote frees them to watch the load and the station. On assembly stations, radio control is usually the more productive and safer choice.

    Frequency Inverter Travel and Hoist

    Stepless speed control with defined acceleration and crawl steps lets the operator place loads without shock. On machined powertrain components, controlled set-down is a quality requirement, not a comfort feature.

    Anti-Sway and Positioning Control

    Closed-loop anti-sway and target positioning reduce swing, shorten waiting at the station and protect fixtures and parts. Encoder feedback and slow-approach zones place the hook within repeatable tolerances cycle after cycle.

    Interlocks and Plant Systems

    Where cranes share space with conveyors, robots or skid systems, interlocks, zone limits and signal exchange with the plant controller are engineered into the crane control. The interface scope belongs in the contract, not in site improvisation.

    Duty Class and High-Cycle Assembly Reliability

    Assembly cranes run many small cycles per shift for years. Reliability comes from matching mechanism classifications, brakes and structure to the measured duty — and from designs that can be maintained inside production windows.

    The Default Duty Trap

    Many general-purpose offers are built to infrequent-use classifications. On a station cycling every takt, those mechanisms consume their design life early. Duty class must be specified from the measured cycle profile, never left to the supplier default.

    Fatigue and Structural Allowance

    High-cycle welding details, wheel and rail contact and brake engagement counts are fatigue items. The structure is engineered for the number of cycles the line will actually run, not for a nominal tonnage figure.

    Maintenance-Friendly Design

    Wear parts, brakes and limit systems are arranged for fast access inside short production breaks. Maintenance positions and inspection routes are defined at design stage, because unplanned line stops cost vehicles, not minutes.

    Documentation and Testing

    Structural calculations, test certificates, overload and static load test reports and defined acceptance criteria support commissioning and the plant’s own safety and audit systems. Documentation scope is agreed before production starts.

    Engineering and Supply Scope for Assembly Plant Projects

    An automotive assembly crane project typically covers several crane families at once: standard and European-style single girder cranes for line-side and machining areas, double girder cranes for the press shop and powertrain, and suspended systems feeding the final assembly stations. Henan Mine Crane plans such projects around a common engineering baseline, so that control behaviour, spares and documentation stay consistent across the different areas of the plant.

    A complete supply definition states the crane structure and machinery, the hoist and control system, the runway or suspension interface, conductor systems, the safety functions required at each station, the overload and acceptance testing regime, and the delivery, installation and commissioning responsibilities. Where the plant’s own engineering team installs, supervision, commissioning and load testing remain part of the package.

    Standard configurations are typically delivered within 30 to 45 days after drawing approval, with engineered or automation-equipped cranes on confirmed project schedules. Multi-crane programs are sequenced against the plant’s shutdown and ramp-up calendar.

    electric single girder suspension crane for automotive final assembly line-side supply
    A single girder suspension crane of the type used for line-side material supply at automotive assembly stations.

    ASSEMBLY CAPACITY COVERAGE

    0.5 t – 50 t

    CRANE FAMILIES APPLIED

    6 Product Platforms

    STANDARD DELIVERY

    30 – 45 Days

    ENGINEERED DUTY RANGE

    A3 – A6 Assembly Service

    Automotive Assembly Crane Price Reference

    Current market positions for Chinese-manufactured crane equipment, expressed as indicative ranges. An equipment price covers the crane ex-works; an installed project adds runway or suspension steel, conductor systems, freight, duty, installation and commissioning.

    Crane Scope Typical Capacity Indicative Equipment Price What Moves the Number
    Suspended workstation system 0.125–2 t US$1,800 – 8,000 per system Rail length covered, number of bridges, hoist grade
    Line-side monorail or suspended crane 0.25–10 t US$1,800 – 9,000 Track routing, switches, curves, suspension points
    Single girder assembly crane 1–20 t US$2,900 – 22,000 Span, lift height, hoist grade, control mode
    European-style single girder crane 3.2–20 t class US$13,000 – 49,000 Duty rating, low-headroom design, speed control level
    Double girder assembly and powertrain crane 5–20 t US$10,000 – 35,000 Span, dual speed levels, cabin or radio control
    Press shop die handling crane 20–50 t US$28,000 – 80,000 Span, slow precise speed ratios, special duty build
    Runway and rail package Per bay length US$5,000 – 20,000 Bay length, rail profile, structural reinforcement
    Freight, duty and installation On equipment price Typically +20 – 50 % on FOB Destination, installation scope, local certification

    Comparing offers on an equipment price alone understates the real decision. Normalize every quotation to the same supply boundary — capacity including fixtures, span, lift, control mode and speed levels, conductor systems, installation, testing and documentation — before comparing numbers. A complete installed assembly crane system typically lands 30–60 % above the ex-works equipment figure.

    Quote Information and Frequently Asked Questions

    A complete enquiry should state the production area, the loads at each lifting point including fixtures and tooling, takt time, required positioning accuracy, building dimensions and roof steel condition, power supply, destination and the required supply boundary.

    Load and Station Data

    Part weights with fixtures and tooling at every lifting point, heaviest combination, lift frequency per station and the full production shift pattern.

    Building and Geometry Data

    Clear height, span or rail centers, travel lengths, roof steel or runway capacity, conveyor and automation positions, and the hook coverage each station requires.

    Process and Accuracy Data

    Positioning tolerance at set-down, acceptable residual sway, required speeds and inching behaviour, and any interlocks with conveyors, robots or plant systems.

    Commercial and Site Data

    Voltage and frequency, destination and Incoterm, installation responsibility, required certifications and documentation, spares level and requested delivery schedule.

    What crane does an automotive assembly plant use?

    Assembly plants use a combination of systems: single and European-style single girder bridge cranes for line-side and machining areas, double girder cranes for press shops and powertrain handling, double trolley cranes for long parts, and suspended workstation systems for ergonomic part supply at stations.

    How is an assembly crane different from a standard workshop crane?

    The difference is duty and control, not just tonnage. Assembly cranes are classified for high cycle counts tied to takt time, use stepless speed control with crawl and anti-sway behaviour for repeatable positioning, and integrate with conveyors, robots and plant safety systems.

    Single or double girder for an assembly line?

    Most line-side loads up to 20 t are served by single girder cranes at lower cost. Double girder becomes the right choice for loads above 20 t, for maximum hook height under the roof, or for stiff, precise handling of press dies, skids and powertrain modules.

    How much does an automotive assembly crane cost?

    Current market positions place single girder assembly cranes between roughly US$2,900 and 22,000 on an equipment basis, European-style single girder systems between US$13,000 and 49,000, and double girder assemblies from about US$10,000 for lighter units to US$80,000 for press shop die handling. Freight, duty and installation typically add 20–50 % over the equipment price.

    Can the crane work with conveyors and robots in the same bay?

    Yes, when it is engineered that way. Hook coverage is mapped against conveyor and robot positions, zone limits and interlocks are built into the crane control, and signal exchange with the plant controller is defined in the interface specification before manufacture.

    What is the delivery time?

    Standard configurations are typically delivered within 30 to 45 days after drawing approval. Cranes with anti-sway positioning, line integration or multi-crane program sequencing run on confirmed project schedules agreed before production starts.
    Get an Automotive Assembly Crane Engineered for Your Line

    Send the station loads, takt time and building dimensions and receive a configured proposal with duty classification, control system, interface definitions, documentation and a delivery schedule for your production area.

    Henan Mine CraneDiscuss your requirements ↗
  • Automated Warehouse Stacker Crane

    Automated Warehouse Stacker Crane

    Automated Warehouse Stacker Crane

    Henan Mine Crane · Automated Storage and Retrieval Equipment

    Automated Warehouse Stacker Crane

    Henan Mine Crane supplies rail-guided automated warehouse stacker cranes for high-bay storage and retrieval systems. Each machine is engineered around the load unit, rack geometry, aisle length, storage height, required throughput and warehouse-control architecture.

    Available configurations include single-column, double-column, track-switching, turnout and lightweight box-type structures, with high-speed anti-sway control, precise rack-level positioning, protected fork transfer and optional energy feedback.

    Automated warehouse stacker crane operating in a high-bay ASRS aisle
    Rail-guided stacker crane for automated high-bay storage and retrieval. Final structure, load handling device and motion performance are project-specific.
    APPLICATION

    High-Bay AS/RS Warehouses

    STRUCTURES

    Single or Double Column

    LOAD TRANSFER

    Project-Selected Fork System

    SYSTEM INTERFACES

    WMS · WCS · PLC · Conveyor

    Automated Stacker Crane for High-Bay Warehouse Operations

    An automated warehouse stacker crane travels on a fixed aisle rail, positions a lifting carriage at the required rack level and transfers pallets, totes, containers or special load carriers between storage locations and conveyor interfaces. A coordinated control system manages long travel, vertical lifting and fork movement as one automated storage-and-retrieval cycle.

    The machine forms part of a complete AS/RS rather than operating as isolated lifting equipment. Rack tolerances, rail alignment, conveyor handshakes, load identification, WMS/WCS task logic, safety zoning and recovery procedures are defined as system interfaces during engineering.

    Equipment boundary: An AS/RS stacker crane retrieves unit loads inside rack aisles. It is a different equipment category from an overhead warehouse crane, which handles suspended industrial loads across an open bay.

    Automated Warehouse Stacker Crane Applications

    Pallet High-Bay Storage

    Automated inbound, storage, relocation and outbound handling for standardized pallets in high-density rack systems.

    Tote and Container Storage

    Lightweight configurations for totes, bins, containers and smaller load units requiring compact aisle geometry and frequent cycles.

    Production Buffer Warehouses

    Controlled storage between manufacturing processes, with task exchange between production planning, conveyors and warehouse control.

    Special Load-Carrier Systems

    Project-specific forks, supports, sensors and transfer logic for non-standard carriers, containers or process fixtures.

    Automated Warehouse Stacker Crane Specifications

    The stacker crane specification is developed from the complete warehouse operating model. Final values are stated in the approved technical schedule, interface documents and acceptance plan.

    Specification Project Definition Engineering Significance
    Load unit Pallet, tote, container or special carrier dimensions, payload, centre of gravity and stability Defines carriage, fork, clearance, sensor and support requirements
    Rated payload Maximum and typical load, including carrier and handling-device interfaces Establishes structural, drive, braking and transfer demand
    Warehouse geometry Storage height, aisle length and width, rack levels, interface positions and maintenance zones Defines mast arrangement, rail path, travel envelope and hook-up points
    Load handling device Fork type, extension depth, transfer direction, stroke, support surface and load detection Controls rack interface, cycle time and transfer protection
    Throughput and duty Inbound and outbound rate, single and dual cycles, peak profile, operating hours and load distribution Determines speed, acceleration, motor duty, availability strategy and machine quantity
    Motion performance Travel, lift and fork speeds, acceleration, settling time and positioning criteria Connects throughput with structural response and rack-level transfer accuracy
    Control interfaces WMS, WCS, PLC, network, conveyor handshake, barcode or RFID and data records Defines command ownership, status exchange, traceability and recovery logic
    Environment and service Temperature, humidity, dust, fire strategy, access, spare parts and availability target Defines component protection, maintenance concept and lifecycle support scope

    Selection Considerations

    01 / LOAD UNIT

    Carrier and Payload Definition

    Load-unit dimensions, weight range, centre of gravity, underside geometry, stability and allowable overhang establish the transfer interface.

    02 / RACK AND AISLE

    Storage Geometry and Tolerances

    Rack elevations, aisle length, transfer clearances, rail alignment, guide tolerances and maintenance access determine the machine envelope.

    03 / THROUGHPUT

    Cycle Model and Peak Demand

    Single-cycle, dual-cycle and peak task profiles establish motion performance, machine quantity, buffering and availability requirements.

    04 / TRANSFER

    Fork Depth and Handover

    Single-depth, double-depth and special transfer arrangements require different fork stroke, detection, support and cycle-time calculations.

    05 / CONTROLS

    Automation Responsibility

    The interface schedule assigns WMS, WCS, PLC, network, identification, conveyor, cybersecurity and acceptance-testing responsibilities.

    06 / LIFECYCLE

    Availability and Recovery

    Maintenance access, diagnostic depth, spare parts, recovery procedures and redundancy are aligned with the required system availability.

    Automated Warehouse Stacker Crane Compared with Other Warehouse Handling Configurations

    Configuration selection is based on the same load-unit data, storage geometry, throughput model, control boundary and availability target. Equipment cost is evaluated together with rack density, aisle quantity, transfer stations, software integration and lifecycle access.

    Configuration Operating Arrangement Application Fit Critical Procurement Criteria
    Single-Column Stacker Crane One mast supports the lifting carriage and handling device Suitable payload, storage height and dynamic duty where lower machine mass and a compact aisle are priorities Mast deflection, carriage guidance, acceleration, settling time and maintenance access
    Double-Column Stacker Crane Two columns provide a guided structural frame for the carriage Heavier loads, taller storage, higher stiffness demand or intensive operating cycles Machine envelope, rail loads, structural stiffness, energy demand and service access
    Track-Switching or Turnout System A machine transfers between compatible aisle rail paths Multiple aisles where the throughput model supports shared equipment and transfer time Switch geometry, route availability, control interlocks, recovery access and capacity during maintenance
    Conventional Forklift Storage Operator-driven mobile handling within warehouse aisles Flexible layouts, lower automation requirements and applications where manual traffic is acceptable Aisle width, storage height, labour, traffic management, inventory accuracy and long-term operating cost
    Overhead Warehouse Crane Suspended-load lifting across an open warehouse bay Machinery, steel, tooling and industrial goods that require overhead hook coverage rather than rack-aisle retrieval Building support, hook coverage, lifting attachment, duty and interaction with racks or traffic

    Automated Storage and Retrieval Operating Cycle

    A complete cycle combines material-flow commands, equipment status, load identification and controlled motion. The operating sequence is configured to match the warehouse software architecture and the physical interfaces at every storage and transfer position.

    STEP 01

    Task Release

    The warehouse system releases a validated storage, retrieval or relocation task with the required load and destination data.

    STEP 02

    Load Handover

    Conveyor and stacker-crane controls confirm load identity, position, readiness and transfer permission before movement begins.

    STEP 03

    Coordinated Travel

    Long travel and lifting are coordinated to approach the assigned rack location while controlling structural response and settling time.

    STEP 04

    Protected Transfer

    Position and occupancy conditions are checked before the fork extends, transfers the load and returns to its travel position.

    STEP 05

    Status Confirmation

    Completion, location and equipment status are returned to the control hierarchy for inventory records and the next task assignment.

    Structural Configurations Engineered for the Storage System

    Single-Column and Double-Column Designs

    Single-column construction can reduce moving mass and support compact aisle arrangements when payload, storage height and dynamic behaviour permit. Double-column construction provides a framed carriage guidance arrangement for applications requiring greater stiffness, heavier load handling or demanding operating cycles.

    The final structure is selected through load analysis, aisle geometry, dynamic response, positioning requirements, drive duty and maintainability. Lightweight box-type structural members may be applied where mass reduction and rigidity must be balanced.

    Configurable automated warehouse stacker crane structure
    Structural arrangement is matched to payload, storage height, aisle geometry, throughput and service access.
    Stacker crane mast carriage and fork assembly for warehouse automation
    The mast, carriage, guidance and load-handling device are engineered as one motion and transfer system.

    Fixed-Aisle, Track-Switching and Turnout Arrangements

    A fixed-aisle stacker crane provides dedicated access and predictable capacity within one aisle. Track-switching and turnout arrangements allow a compatible machine to serve more than one aisle when the throughput calculation, route availability and recovery strategy support shared equipment.

    Multi-aisle operation requires coordinated route control, transfer-position interlocks and a capacity assessment covering both normal production and planned maintenance conditions.

    High-Speed Motion, Anti-Sway Control and Precise Positioning

    Warehouse throughput depends on more than maximum speed. Acceleration, deceleration, structural response, settling time and final transfer accuracy must work together across the full aisle and lifting range. Henan Mine Crane applies static and dynamic finite-element analysis to evaluate structural behaviour and support the selected motion profile.

    Automated warehouse stacker crane engineered for stable high-speed travel

    Controlled Dynamic Response

    Motion profiles and anti-sway control reduce unnecessary oscillation during travel and lifting, supporting shorter settling time and stable approach to the target rack position.

    Automated stacker crane positioning at a high-bay rack location

    Rack-Level Positioning

    Position feedback, controlled approach and transfer permissives align the carriage and fork with the assigned storage or handover point before load movement is authorized.

    Performance definition: Travel speed, lift speed, fork cycle, acceleration and positioning criteria are confirmed from the throughput model, rack tolerances, payload behaviour and required machine availability. They are not treated as isolated catalogue values.

    Fork Transfer and Load Protection

    Automated warehouse stacker crane fork and load transfer interface
    Fork geometry, extension depth, sensors and transfer logic are configured around the load carrier and rack interface.

    The load-handling device is specified from the carrier underside, storage depth, support arrangement, permitted clearances and transfer direction. Single-depth, double-depth and special telescopic solutions require different fork strokes, deflection control, detection logic and cycle calculations.

    • ✓Transfer authorization based on machine position, fork status and interface readiness
    • ✓Fork anti-push-off protection for controlled handling at the rack location
    • ✓Load-presence and storage-position conditions integrated into the project control logic
    • ✓Protected transition between storage racks, stacker crane and conveyor handover stations

    Space Utilization and Energy Management

    A rigid-flexible column concept and compact equipment envelope can support high-density storage where the structural calculation, rack geometry and service clearances permit. The layout is coordinated with the aisle rail, top guidance, maintenance access, buffer conveyors and fire-protection strategy.

    An optional energy-feedback module can return regenerative energy produced during lowering and deceleration to the electrical system. Its application is assessed against motion frequency, load profile, electrical architecture and project energy objectives.

    Automated warehouse stacker crane fork and load transfer interface
    Machine envelope and maintenance zones are integrated with rack and aisle planning.

    WMS, WCS, PLC and Conveyor Integration

    System integration is defined through an interface schedule covering command ownership, data exchange, equipment handshakes, alarm handling, operating modes and recovery procedures. Responsibility boundaries are established before software development and verified during staged testing.

    Automated warehouse stacker crane integrated with high-bay racks and material flow equipment
    The stacker crane is integrated with rack, conveyor, identification, control and warehouse-management functions.
    System Layer Primary Function Interface Definition
    WMS Inventory, location and warehouse-task management Task identifiers, load data, origins, destinations, completion status and exception records
    WCS Material-flow coordination and equipment task dispatch Queue logic, route selection, interface availability, task priority and recovery coordination
    Stacker Crane PLC Machine sequence, motion control, interlocks and diagnostics Task acceptance, operating permission, position, load status, alarms and machine state
    Conveyor and Identification Physical handover and load verification Ready/busy signals, load presence, transfer permission, barcode or RFID data and mismatch handling
    Operator and Maintenance Interface Status visibility, permitted control and diagnostic support User roles, alarm history, manual modes, reset conditions, maintenance functions and event records

    Safety, Interlocks and Controlled Recovery

    Safety functions are established through the project risk assessment, equipment layout and operating concept. The control philosophy separates normal automatic operation, authorized manual functions, maintenance access and fault recovery.

    Motion Interlocks

    Travel, lifting and fork movements are permitted only when the defined machine and interface conditions are satisfied.

    Transfer Protection

    Position, load and handover signals are evaluated before rack or conveyor transfer, with fork anti-push-off protection integrated into the sequence.

    Access Control

    Fenced zones, access points and maintenance procedures are coordinated with the warehouse layout and applicable project requirements.

    Fault Recovery

    Alarm classification, safe reset conditions, manual recovery steps and responsibility boundaries are documented for service personnel.

    Project compliance: Applicable machinery, electrical, fire, building and workplace requirements are identified for the installation country and facility. The confirmed compliance scope is stated in the technical agreement.

    Engineering, Manufacturing and Project Documentation

    Henan Mine Crane developed its intelligent stacker-crane platform jointly with the Beijing Research Institute of Hoisting and Conveying Machinery. Product engineering combines warehouse-layout coordination, static and dynamic structural analysis, motion-control development, load-transfer design and system-interface definition.

    Project Engineering

    Layout review, equipment boundary, performance calculation, interface schedule, structural verification and maintainability assessment.

    Manufacturing Control

    Fabrication, assembly, drive installation, electrical integration and inspection are managed against the approved project specification.

    Technical Deliverables

    Agreed drawings, parameter schedules, interface records, operating information, maintenance documentation and acceptance records.

    Manufacturing capabilities and production resources are available on the Henan Mine Crane factory page.

    Installation, Commissioning and Acceptance

    01. Interface Readiness

    Rail, rack, power, network, conveyor, identification and access conditions are checked against approved interface data.

    02. Mechanical and Electrical Setup

    Machine alignment, guidance, drives, sensors, control panels and communication links are installed and verified.

    03. Functional Commissioning

    Operating modes, motion, positioning, fork transfer, interlocks, alarms and system handshakes are commissioned in stages.

    04. Performance Acceptance

    The agreed test plan verifies functions, interfaces, representative load handling, throughput conditions and recovery procedures.

    Acceptance criteria, test loads, test data, operating conditions, attendance and responsibility boundaries are stated in the contract documentation before site testing.

    Maintenance and Lifecycle Support

    Maintenance planning begins during layout and equipment engineering. Safe access, inspection points, component replacement paths, diagnostic information and recovery procedures are coordinated with the required operating availability.

    Inspection Planning

    Scheduled checks aligned with duty, environment, critical assemblies and operating records.

    Diagnostics

    Alarm history, status information and defined troubleshooting paths support structured fault isolation.

    Spare Parts

    Recommended commissioning, operational and critical spares can be defined from the service strategy.

    Training

    Operating, maintenance and recovery training can be included within the agreed delivery scope.

    Information Required for an Automated Stacker Crane Proposal

    A technically comparable proposal requires a defined warehouse operating basis. Preliminary data may be used for concept development, followed by an approved interface schedule for detailed engineering.

    Load and Carrier Data

    Dimensions, maximum and typical weight, centre of gravity, underside arrangement, stability, overhang and identification method.

    Rack and Building Layout

    Storage height, aisle length and width, rack levels, storage depth, rail path, top guidance, transfer stations and service zones.

    Throughput Model

    Inbound and outbound rates, single and dual cycles, peak duration, task distribution, working hours and availability target.

    System Interfaces

    WMS/WCS architecture, PLC and network requirements, conveyor handshakes, barcode or RFID, data ownership and cybersecurity conditions.

    Site Conditions

    Installation location, temperature, humidity, dust, electrical supply, fire strategy, access restrictions and applicable regulations.

    Delivery Boundary

    Equipment, rails, controls, software, conveyors, installation, commissioning, testing, training, documentation and spare-parts scope.

    Automated Warehouse Stacker Crane FAQ

    What is an automated warehouse stacker crane?

    It is a rail-guided storage and retrieval machine that travels within a warehouse aisle, lifts a carriage to rack level and transfers unit loads between storage locations and material-flow interfaces under automatic control.

    When is a single-column design appropriate?

    Single-column construction may be selected when the payload, storage height, stiffness, motion profile and service-access requirements support a lighter and more compact structure. Engineering verification determines its suitability.

    Can one stacker crane serve multiple aisles?

    Track-switching or turnout configurations can serve compatible aisle paths. The decision requires verification of transfer time, route availability, peak throughput, recovery access and capacity during maintenance.

    Does the stacker crane connect with an existing WMS or WCS?

    Integration can be developed around an existing warehouse software environment when protocols, task ownership, data fields, alarm handling, network conditions and testing responsibilities are defined in the interface schedule.

    How is stacker-crane throughput determined?

    Throughput is calculated from aisle geometry, storage-location distribution, transfer time, travel and lift motion, fork cycle, buffering, single and dual cycles, peak demand and equipment availability. Maximum travel speed alone does not define system capacity.

    Which load data are essential for fork selection?

    Required data include carrier dimensions, payload range, underside geometry, support positions, centre of gravity, stability, overhang, storage depth, permitted clearance and transfer direction.

    Can energy recovery be included?

    An optional energy-feedback module can recover regenerative energy during lowering and deceleration. Feasibility depends on the motion profile, operating frequency, load distribution and facility electrical system.

    What determines the final stacker-crane price?

    Major cost drivers include payload, storage height, aisle length, machine quantity, structural configuration, fork depth, performance, control scope, software interfaces, site conditions, installation, testing, training and spare-parts requirements.

    Request an Automated Warehouse Stacker Crane Quote

    Henan Mine Crane develops project-specific stacker-crane proposals from load-unit data, warehouse geometry, throughput, automation interfaces, site conditions and delivery boundaries.

    Henan Mine CraneDiscuss your requirements ↗
  • Aluminum Smelter Multifunction Crane

    Aluminum Smelter Multifunction Crane

    Aluminum Smelter Multifunction Crane

    Henan Mine Crane · Potroom Process Equipment

    Aluminum Smelter Multifunction Crane

    An aluminum smelter multifunction crane is an engineered pot tending machine for prebaked-anode reduction cells. The traveling bridge, tool trolley and dedicated process modules can be configured for crust breaking, anode changing, bath cleaning, alumina or cover-material feeding, aluminum tapping support, busbar-related lifting and pot maintenance.

    Henan Mine Crane develops each PTM around the pot technology, anode geometry, cell pitch, potroom runway, required operations, production cycle and environmental conditions. Tool capacities and duty requirements are specified separately because a single crane tonnage does not define a multifunction potroom machine.

    aluminum smelter multifunction crane for electrolytic potroom operations
    Potroom process equipment configured for the operating sequence, clearances and environmental demands of aluminum electrolysis.

    EQUIPMENT FAMILY

    PTM / Pot Tending Crane

    PRIMARY APPLICATION

    Prebaked-Anode Potlines

    FUNCTION PACKAGE

    Selected by Pot Process

    PRICE BASIS

    Engineered Project Quote

    What Is an Aluminum Smelter Multifunction Crane?

    The terms aluminum smelter multifunction crane, pot tending machine, pot tending crane and PTM crane commonly describe a bridge-mounted process machine that services reduction cells in an aluminum potroom. Unlike a standard overhead crane, the PTM carries a coordinated set of tools and handling mechanisms matched to electrolysis operations.

    A complete machine may combine an anode handling unit, crust breaker, bath or residue removal tool, material feeding system, aluminum tapping trolley or tapping interface, auxiliary hoist, rotating tool carriage and operator cabin. The final arrangement depends on which operations are assigned to the PTM and which remain with separate plant equipment.

    Process Machine

    The PTM performs repeatable pot operations; it is not only a lifting bridge with a hook.

    Multi-Tool Platform

    Each mechanism has its own load, reach, motion, duty, accuracy and process interface.

    Potline-Specific Design

    Bridge geometry, tool envelope and control logic follow the actual cell technology and bay layout.

    Harsh-Duty Protection

    Electrical, thermal, dust, fume and magnetic-field conditions are part of the design basis.

    Selection Considerations

    01 / POT TECHNOLOGY

    Cell Geometry and Pitch

    Define cell type, centerline pitch, hood arrangement, anode layout, access side, working zones and no-go envelopes.

    02 / ANODE SYSTEM

    Anode and Clamp Data

    Record new and spent anode mass, dimensions, stem arrangement, clamp interface, extraction stroke and placement tolerance.

    03 / REQUIRED TOOLS

    Process Function Schedule

    List crust breaking, feeding, anode changing, bath cleaning, tapping, busbar work, cover handling and maintenance functions.

    04 / PRODUCTION

    Cycle and Availability

    State pots served, shifts, planned tool cycles, peak demand, standby philosophy, recovery time and maintenance windows.

    05 / POTROOM

    Runway and Clearances

    Verify rail span, elevation, approaches, wheel-load limits, longitudinal geometry, building deflection and erection route.

    06 / ENVIRONMENT

    Heat, Dust, Fumes and Field

    Supply measured ambient and radiant heat, magnetic-field map, conductive dust, fluoride fume and ventilation conditions.

    07 / CONTROL

    Manual, Assisted or Automated

    Define cabin, remote station, tool interlocks, pot identification, positioning, data exchange and automatic sequence boundaries.

    08 / SUPPLY SCOPE

    Interfaces and Acceptance

    Fix the limits for runway, power, compressed air, fume extraction, installation, testing, training, spares and documentation.

    A reliable quotation requires a tool-by-tool process specification. Bridge rated load alone cannot establish anode handling force, crust-breaker energy, feed volume, tapping arrangement, auxiliary-hoist duty or required production throughput.

    Aluminum Smelter Multifunction Crane vs. Related Crane Types

    Pot tending, anode logistics, energized-area maintenance and molten-aluminum transfer are separate duties. The following equipment families can operate within one smelter, but they are not interchangeable.

    Equipment Primary Duty Process Tools Selection Boundary
    Aluminum Smelter Multifunction Crane Integrated tending of prebaked-anode reduction cells Multiple dedicated tools selected for the pot process Correct choice when repeated cell operations must be combined on one traveling platform
    Anode Carbon Block Stacking Crane Anode storage, stacking and warehouse transfer Multi-block gripper or project-specific clamp Supports carbon logistics but does not change anodes at an energized reduction cell
    Insulated Overhead Crane Maintenance or material lifting where electrical isolation is required Hook or approved lifting attachment Insulation alone does not provide PTM process tooling or pot-tending sequences
    Double-Trolley Insulated Crane Coordinated insulated lifting with two trolley mechanisms Hooks or dedicated lifting beams Suitable for selected handling duties, not a substitute for a rotating multi-tool trolley
    Metallurgical Ladle Crane Molten-metal ladle lifting and transfer Ladle beam, plate hook or project attachment Selected for hot-load transfer; it does not break crust, feed material or change anodes
    General Double-Girder Bridge Crane Plant maintenance and general material handling Hook, beam or other conventional attachment Requires substantial redesign before use near energized cells, fluoride fumes or PTM operations

    Pot Tending Functions and Tool Modules

    The function package must reflect the established pot operating procedure. Not every PTM requires every module, and one tool can require different geometry for different reduction-cell technologies.

    pot tending machine tool system for aluminum electrolysis
    The tool carriage is engineered around the required reach, working envelope, process force and cell access arrangement.

    Crust Breaking and Working-Hole Opening

    A guided breaker opens the electrolyte crust at defined positions. Tool reach, impact requirement, alignment and debris control follow crust condition and cell geometry.

    Anode Changing

    The anode mechanism releases the clamp interface, extracts the spent assembly, handles the replacement anode and positions it at the designated location. Mass, stem form, center of gravity and placement tolerance are essential inputs.

    Bath and Residue Removal

    A cleaning or grab tool can remove crust pieces, residual material and selected bath deposits from the working area before placement of the new anode.

    Alumina and Cover-Material Feeding

    A metered feeding arrangement distributes alumina, fluoride additions or cover material where specified. Storage volume, discharge rate, dust containment and refill interface form part of the procurement data.

    Aluminum Tapping Support

    The PTM can carry or position a tapping trolley, pipe or ladle interface. Vacuum generation, weighing and ladle transport boundaries must be clearly allocated between crane and plant systems.

    Busbar and Pot Maintenance

    An insulated auxiliary hoist or dedicated frame may support approved busbar-related work, hood handling, pot superstructure service and controlled maintenance lifts.

    Auxiliary Handling

    A general auxiliary hoist can handle approved tools, maintenance parts and consumables within the defined capacity, isolation and exclusion-zone rules.

    Machine Architecture, Controls and Automation

    Bridge and Traveling System

    The bridge distributes tool and trolley loads to the potroom runway while providing the required approaches above the cell row. Wheel arrangement, drives, braking and structural stiffness follow the operating spectrum, rail geometry and positioning requirement.

    Tool Trolley and Rotation

    A traversing tool trolley positions the working mechanisms across the cell. A rotating carriage or turret can orient tools to the operating face. Interlocks prevent incompatible motions, tool collision and operation outside approved envelopes.

    PLC, Drives and Positioning

    Variable-frequency drives and PLC control can coordinate bridge, trolley, rotation and tool motions. Pot identification, travel-position feedback, tool-height measurement, load monitoring and sequence permissions can be integrated at the automation level specified for the project.

    Operator Environment

    The cabin location, visibility, filtration, cooling, heat shielding, fume protection and emergency egress are developed from the potroom hazard assessment. Remote or assisted operation can reduce routine exposure while retaining controlled recovery procedures.

    electrolytic aluminum multifunction crane system configuration
    Bridge, trolley, tool systems and controls are coordinated as one potroom process machine.

    Protection for Aluminum Potroom Conditions

    special crane equipment for harsh aluminum smelter potroom conditions
    The protection package must be based on measured heat, field strength, dust, fumes and electrical potential at the operating location.

    Electrical Isolation

    Insulation points, creepage distances, monitoring and maintenance-access rules are selected from the plant electrical design and the maximum credible potential difference. Isolation must cover the complete current path, including tools, hoists, structures and service connections.

    Heat and Fume Resistance

    Heat shields, component location, cooling, material selection and cable protection reduce exposure to hot cell surfaces and radiant heat. Corrosion-resistant finishes, sealed enclosures and protected ventilation address fluoride-bearing fumes.

    Dust and Magnetic-Field Compatibility

    Alumina and carbon dust affect cooling, contacts, sensors and mechanical interfaces. Enclosure rating, filters and cleaning access follow the measured load. Electrical and control components are selected and positioned for the documented magnetic field.

    Safe-Failure Response

    Overload protection, limits, braking, anti-collision, motion interlocks, emergency stops and recovery modes are defined by the project risk assessment. Redundancy is applied where the consequence and governing design basis require it.

    Configurable Technical Specification

    A PTM technical schedule should identify every process mechanism separately. The following procurement fields establish an auditable basis for engineering and quotation.

    Specification Group Required Project Data Engineering Output
    Bridge and Runway Rail span, elevations, approaches, bay length, rail data and allowable reactions General arrangement, wheel loads, clearances and structural design basis
    Anode Tool Anode mass, stem and clamp geometry, stroke, orientation and cycle Rated load, grip interface, force or torque, speed and placement tolerance
    Crust and Cleaning Tools Crust condition, opening position, depth, residue form and cell access Tool energy, reach, guidance, cleaning capacity and exclusion envelope
    Feeding System Material, bulk density, batch volume, discharge pattern and refill station Hopper volume, dosing method, discharge rate and dust-control interface
    Tapping and Auxiliary Hoist Ladle, tapping pipe, vacuum, weighing, maintenance loads and lift paths Interface allocation, hoist SWL, speeds, insulation and controls
    Duty and Performance Pot count, cycles, load spectrum, shifts, availability and standby plan Mechanism classes, motor ratings, thermal checks and throughput model
    Environment and Power Temperature, magnetic field, dust, fumes, voltage, frequency and earthing plan Protection levels, insulation scheme, cooling, materials and power interface
    Controls and Compliance Operating mode, plant communications, required codes and acceptance plan Control architecture, interlock matrix, test procedure and document register

    Final capacities, speeds, classes, protection ratings and automation performance are confirmed after review of the approved operating philosophy, plant data and governing standard. Published values for another potline must not be copied into a new procurement specification without verification.

    Aluminum Industry Project Experience

    Henan Mine Crane aluminum industry lifting project equipment
    Henan Mine Crane aluminum industry equipment covering carbon handling and aluminum electrolysis process requirements.

    Integrated Aluminum Production Lifting Program

    A published Henan Mine Crane aluminum-industry program combines three equipment groups: multifunction suction handling equipment, anode carbon block stacking cranes and multifunction aluminum electrolysis units. The program addresses raw-material movement, carbon-block storage and reduction-cell operations as separate but connected process zones.

    The electrolysis unit integrates shell breaking, anode replacement, residue cleaning and cover-material loading. Sensor-based height measurement, tightening control and automatic operating functions can be applied according to the selected automation scope.

    View Aluminum Industry Project

    Electrolytic Aluminum Crane Configuration

    Henan Mine Crane also publishes an electrolytic-aluminum equipment family for high-duty aluminum liquid transfer, anode handling, cell maintenance and plant material movement. The configuration demonstrates the need to match working class, protection, attachment and control method to the exact process rather than specifying a general metallurgical crane.

    View Electrolytic Aluminum Solution

    Engineering, Manufacturing and Quality Documentation

    Design Basis

    The contract design basis identifies the governing crane, machinery, electrical and structural requirements. Applicable codes may include EN, ISO, IEC, FEM, CMAA or project-specific national standards, but the agreed hierarchy and editions must be fixed before detailed design.

    Engineering Review

    Deliverables can include general arrangement drawings, wheel loads, structural calculations, mechanism selection, tool envelopes, electrical single-line diagrams, PLC architecture, cause-and-effect logic, interlock matrix and utility requirements.

    Fabrication and Inspection

    Material traceability, welding procedures, dimensional checks, nondestructive examination, machining records, assembly inspection, coating controls and purchased-component certificates can be included in the approved inspection and test plan.

    Factory Acceptance

    Factory testing verifies drive direction, brakes, limits, alarms, interlocks, control modes, tool motions and communications to the extent possible before shipment. Site process interfaces are completed during commissioning with approved simulation and live-operation procedures.

    Henan Mine Crane engineered aluminum electrolysis lifting equipment
    Project documentation connects potroom process requirements to mechanical, electrical and control-system acceptance criteria.

    Recommended Document Register

    Technical data sheet · approved general arrangement · interface schedule · wheel-load report · calculation summary · component list · electrical drawings · PLC and network architecture · interlock matrix · inspection and test plan · welding and NDT records · factory test report · installation manual · operation and maintenance manual · spare-parts list · training plan · as-built dossier.

    Installation, Commissioning and Lifecycle Support

    Site Readiness

    Confirm runway survey, rail condition, erection access, lifting plan, utilities, laydown area, shutdown windows and potroom work permits before delivery.

    Mechanical and Electrical Installation

    Bridge assembly, rail alignment, festoon or conductor installation, tool commissioning and plant-network integration follow approved method statements.

    Functional and Process Testing

    Testing progresses from no-load motion and interlocks to proof testing, dry process simulation and controlled potline trials under the agreed acceptance plan.

    Training and Handover

    Operator, electrical, mechanical and automation training should cover normal operation, tool change, alarm response, isolation, recovery and preventive maintenance.

    Maintenance Strategy

    The maintenance plan should be organized by bridge, trolley, process tool, hydraulic or pneumatic system, electrical equipment, cabin services and safety functions. Dust loading, thermal cycling, insulation condition and fume exposure require inspection intervals based on measured service conditions rather than a generic workshop-crane schedule.

    Recommended commissioning spares normally cover critical sensors, seals, filters, contactors, brake wear parts, tool consumables and selected drive or control components. The final list follows failure consequence, local inventory, lead time and the plant standby philosophy.

    Aluminum Smelter Multifunction Crane Price

    There is no dependable standard list price for a complete pot tending machine. Public online advertisements for equipment labeled as an electrolytic aluminum multifunction crane or PTM presently show approximately US$9,000–60,000 per set, while one broad advertisement begins at US$1,000. The range is too wide to represent comparable equipment and frequently lacks a defined tool package, duty, automation scope, runway interface, testing, freight and commissioning.

    These public figures are indicative advertisements only. They are not a Henan Mine Crane selling price, a turnkey smelter budget or a landed installed cost. A technically valid quotation follows review of the potline data and an agreed supply boundary.

    Machine and Tool Package

    Bridge size, tool trolley, anode equipment, breaker, cleaner, feeder, tapping arrangement, hoists, hydraulics and pneumatics.

    Controls and Protection

    PLC, drives, positioning, plant communications, operator cabin, remote operation, insulation, cooling, enclosures and fume protection.

    Project Delivery

    Documentation, testing, packaging, ocean freight, insurance, runway or power scope, installation, commissioning, training and spares.

    Data Required for a Budgetary Quote

    Plant country and destination port · pot technology and layout drawing · runway span and bay length · pot count and production schedule · anode drawings and mass · required tool list · tapping and maintenance scope · environmental measurements · power supply · control and automation level · governing standard · installation responsibility · required delivery date.

    Aluminum Smelter Multifunction Crane FAQ

    Is a pot tending machine the same as an overhead crane?

    It uses an overhead traveling bridge, but it is a process machine with dedicated tools, controls and protections. A conventional hook crane cannot perform the full pot-tending sequence without extensive purpose-specific engineering.

    Which operations can be integrated?

    Typical options include crust breaking, anode changing, residue removal, alumina or cover-material feeding, tapping support, busbar-related lifting and maintenance handling. The approved operating procedure determines the final combination.

    What capacity should be specified?

    Each mechanism requires a separate capacity or performance value. Anode-tool load, auxiliary-hoist SWL, tapping load, breaker energy and feed volume cannot be represented accurately by one headline tonnage.

    Can the PTM be automated?

    Manual, assisted and higher-automation configurations are possible. Automation can include pot identification, position control, height measurement, tool permissions, sequence control, production data exchange and fleet scheduling where the plant interfaces support them.

    How is electrical safety addressed near energized cells?

    The electrical study defines credible current paths and required insulation points. Tool interfaces, hoists, structural sections, service connections, earthing, monitoring and maintenance procedures are coordinated as one isolation system.

    How are fluoride fumes and conductive dust managed?

    Protection can include sealed electrical enclosures, selected materials and coatings, filtered ventilation, cooling, protected cables, serviceable dust barriers and interfaces to plant fume-extraction systems.

    Can an existing potroom runway be retained?

    Retention is possible only after verifying rail geometry, alignment, support condition, wheel-load capacity, longitudinal forces, clearances and erection access against the proposed machine.

    What determines the number of PTMs required?

    Pot count, travel distance, process cycles, peak workload, tool-change time, preventive maintenance, availability target and standby philosophy determine fleet size. A cycle and availability model should support the decision.

    Why is a public online price not a reliable project budget?

    Advertisements rarely define tool count, process performance, duty, automation, environmental protection, runway scope, testing, delivery or commissioning. Two listings with the same nominal tonnage can represent fundamentally different machines.

    What should be included in the final acceptance plan?

    The plan should cover documentation, dimensional inspection, material and welding records, no-load and load tests, limits, brakes, interlocks, tool simulations, communication tests, site process trials, training and handover criteria.

    Request an Aluminum Smelter Multifunction Crane Quote

    Submit the potline layout, anode data, required tool schedule, runway geometry, environmental measurements, control scope and delivery destination. Henan Mine Crane will prepare a configuration and quotation based on the defined process and project supply boundary.

    Henan Mine CraneDiscuss your requirements ↗