Henan Mine Crane · Press Shop, Tooling and Vehicle Production Handling
Automotive Industry Crane Systems
Engineered overhead, underhung, workstation and semi-gantry crane systems for stamping dies, molds, coils, fixtures, powertrain components, vehicle assembly and plant maintenance.
Henan Mine Crane configures each automotive industry crane around the actual load family, production sequence, die-change target, attachment, placement tolerance, duty spectrum, building interface, control architecture, safety zones and contracted project scope.
PRIMARY DUTIES
Dies, Fixtures, Components and Maintenance
PLANT ZONES
Press, Body, Powertrain and Assembly
CRANE OPTIONS
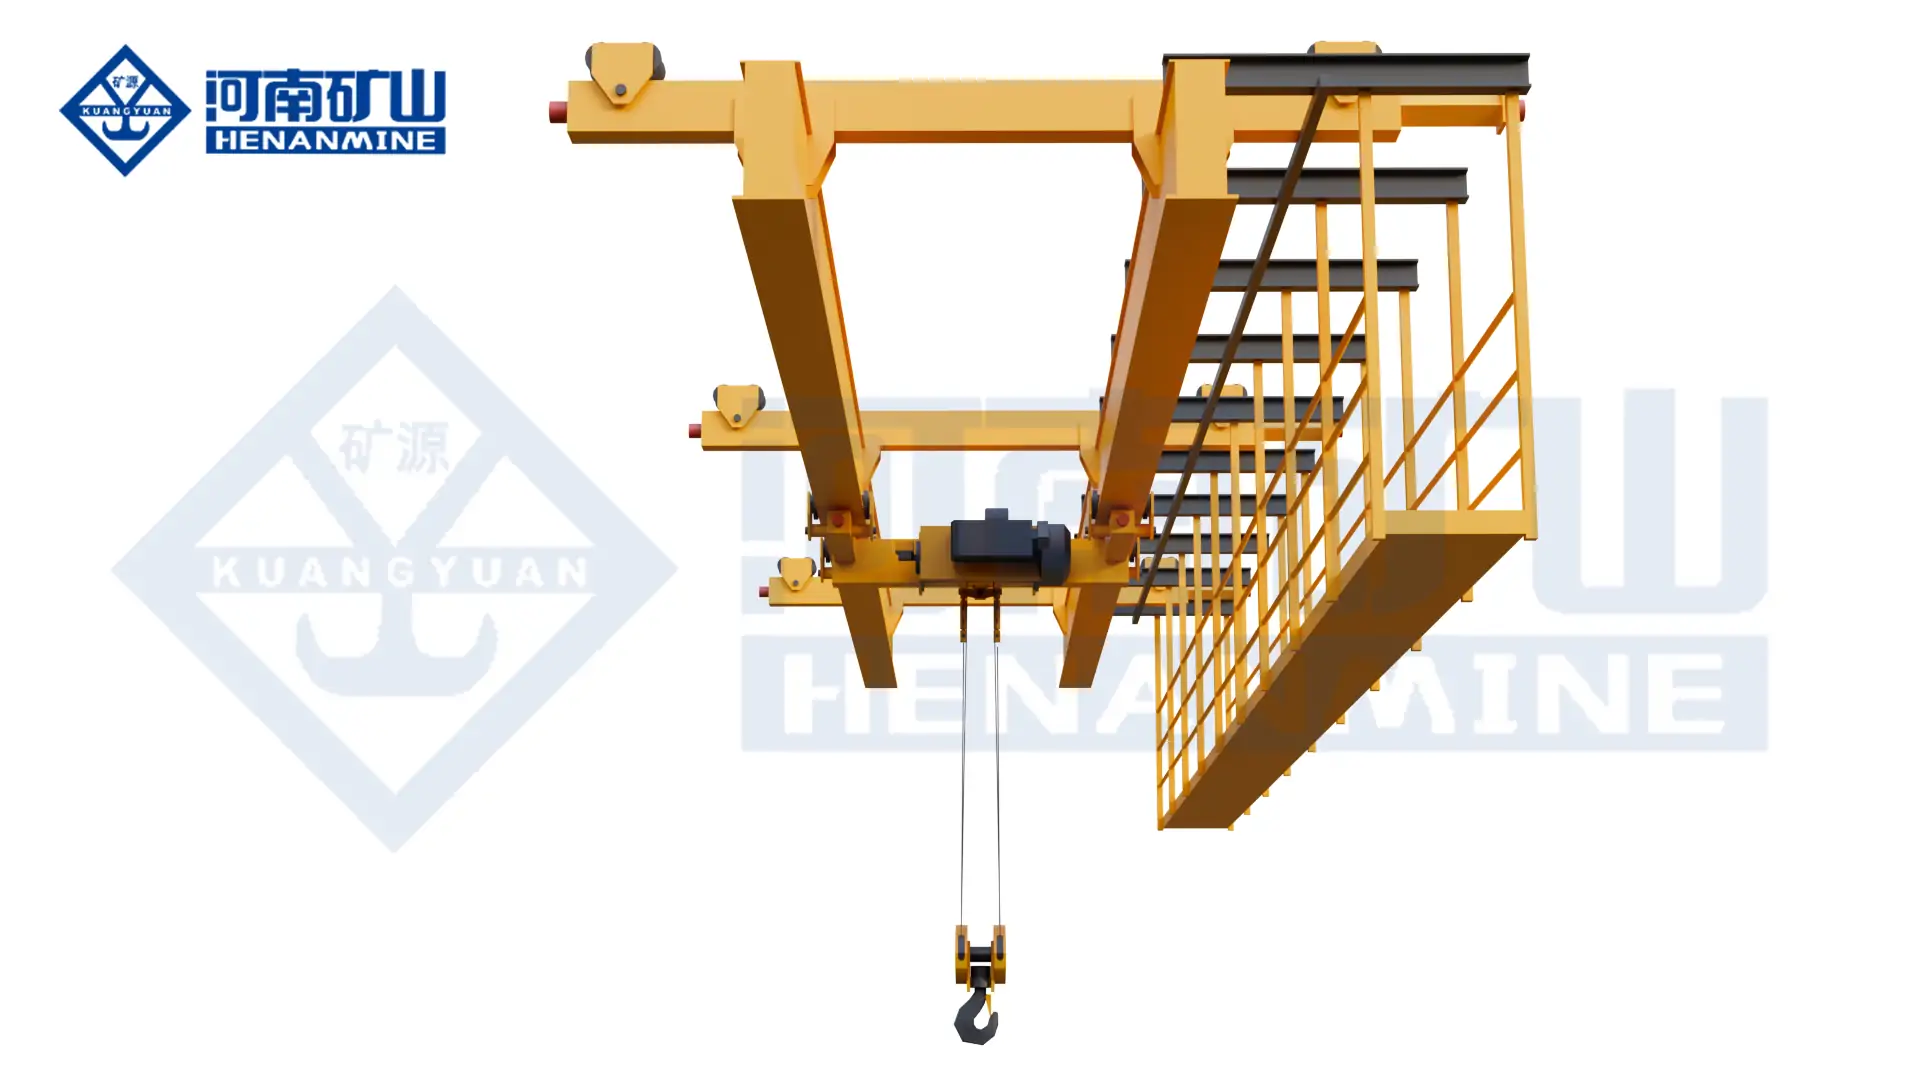
Bridge, Underhung, Workstation or Semi-Gantry
CONTROL LEVELS
Manual, Assisted, Semi-Automatic or Automatic
What Is an Automotive Industry Crane?
An automotive industry crane is an engineered lifting system used in vehicle plants, component factories and tooling facilities. Typical duties include press-die storage and changeover, mold transfer, steel-coil receiving, body fixture handling, robot and conveyor maintenance, engine and transmission assembly, battery-pack movement, end-of-line service and general plant maintenance.
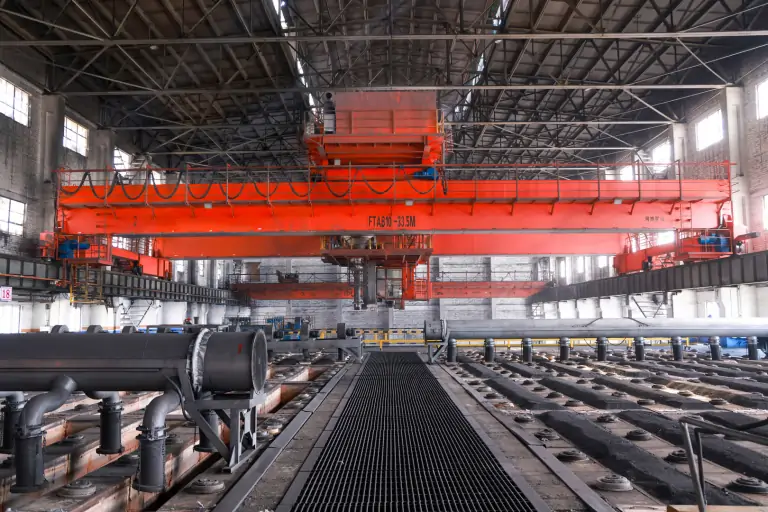
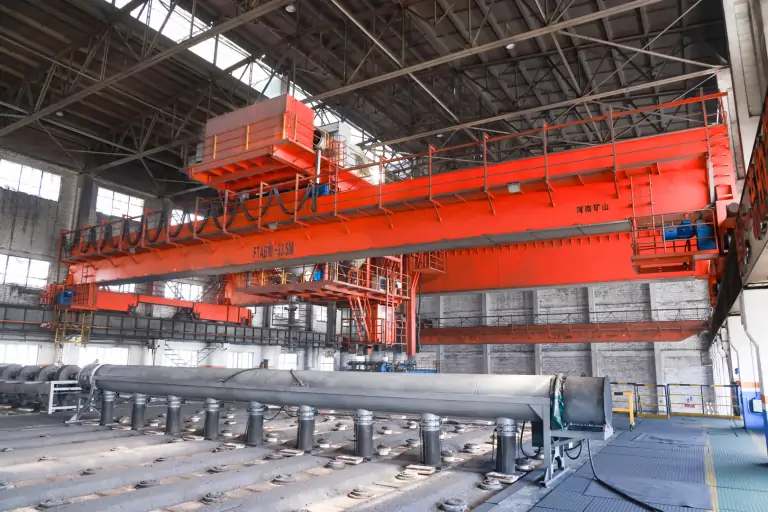
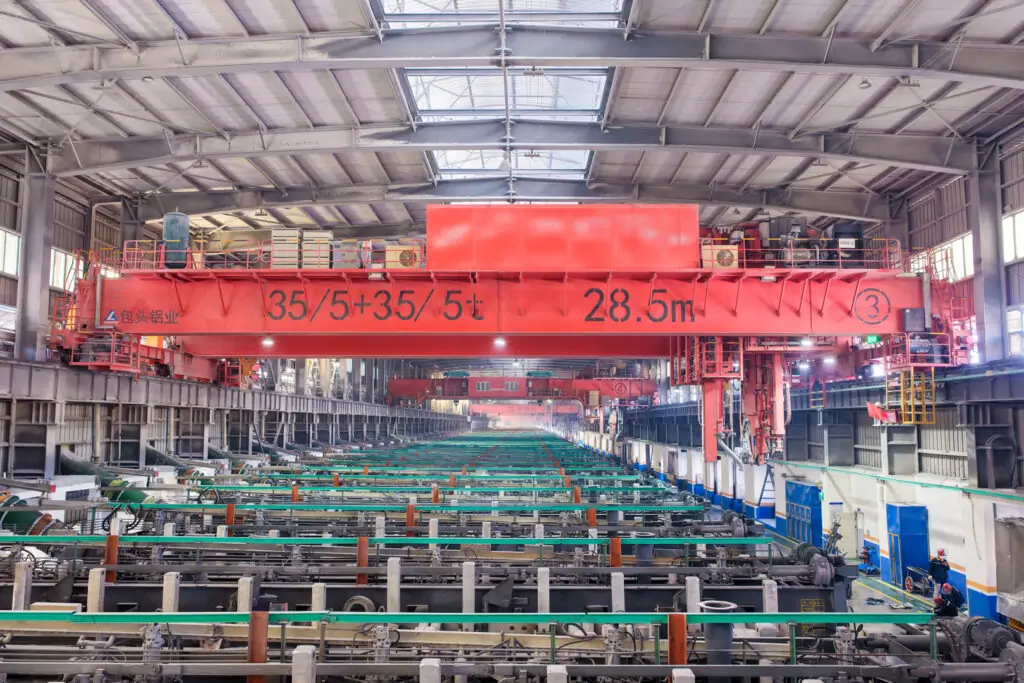
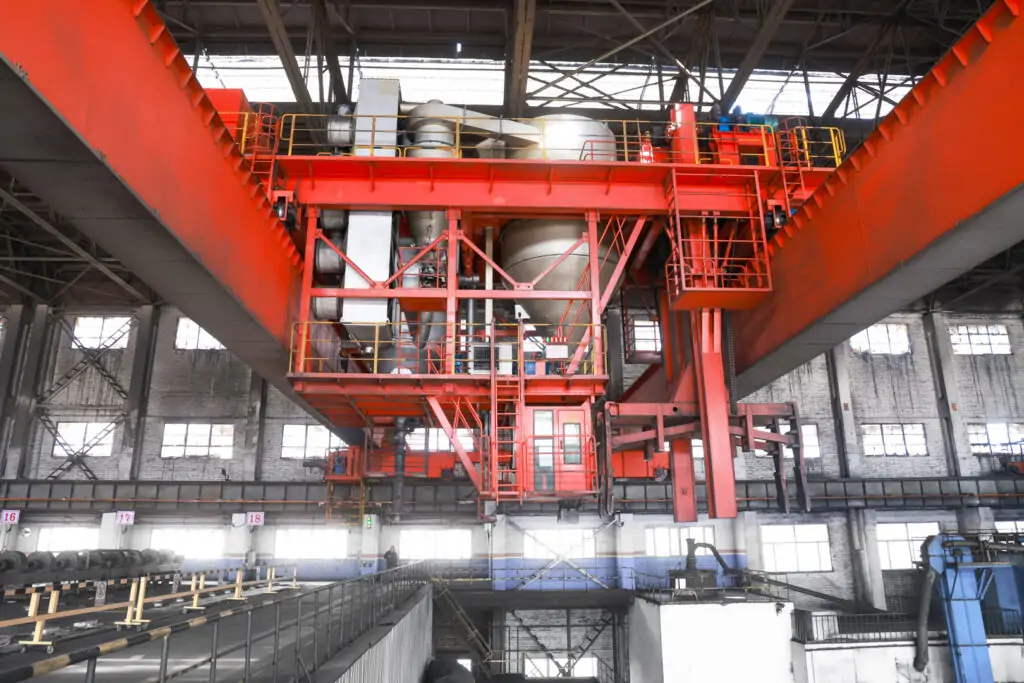
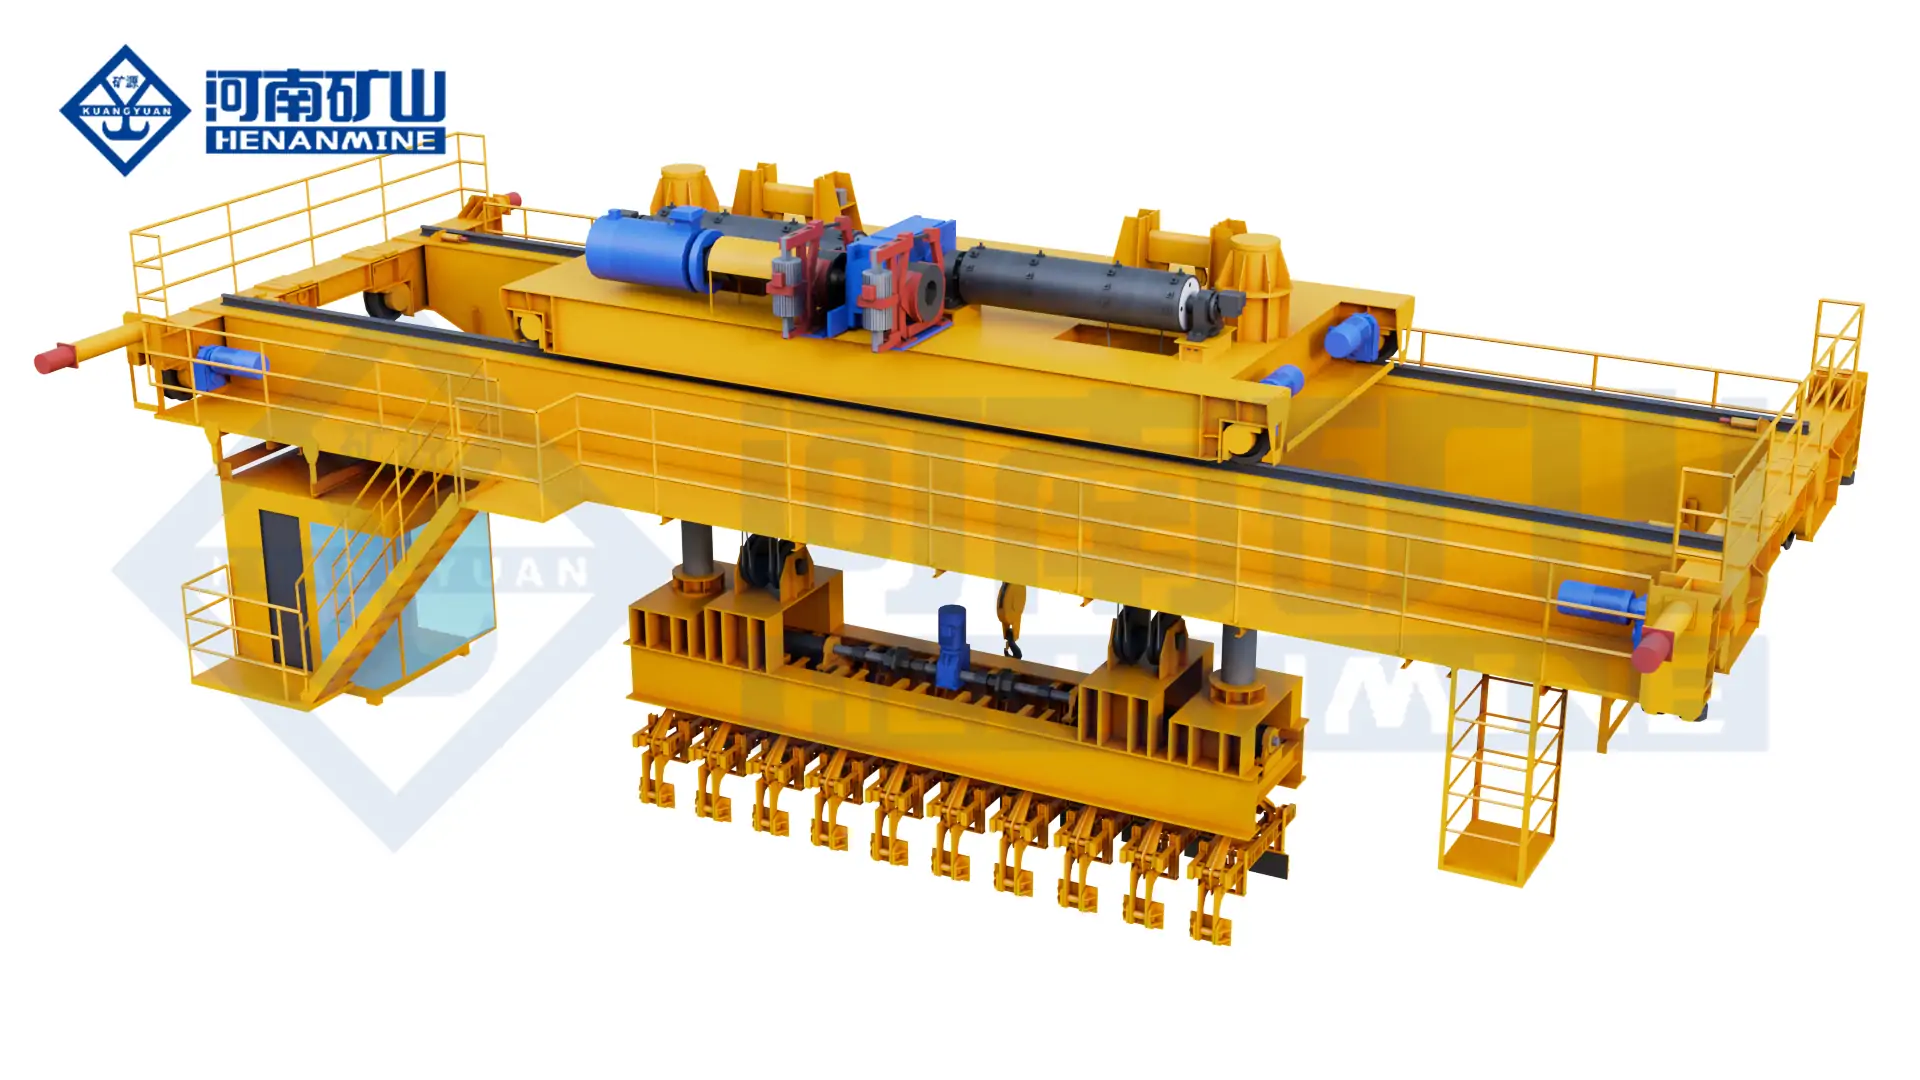
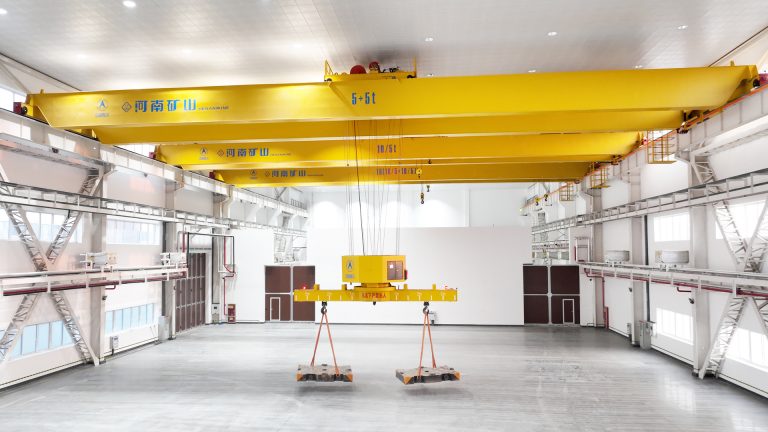
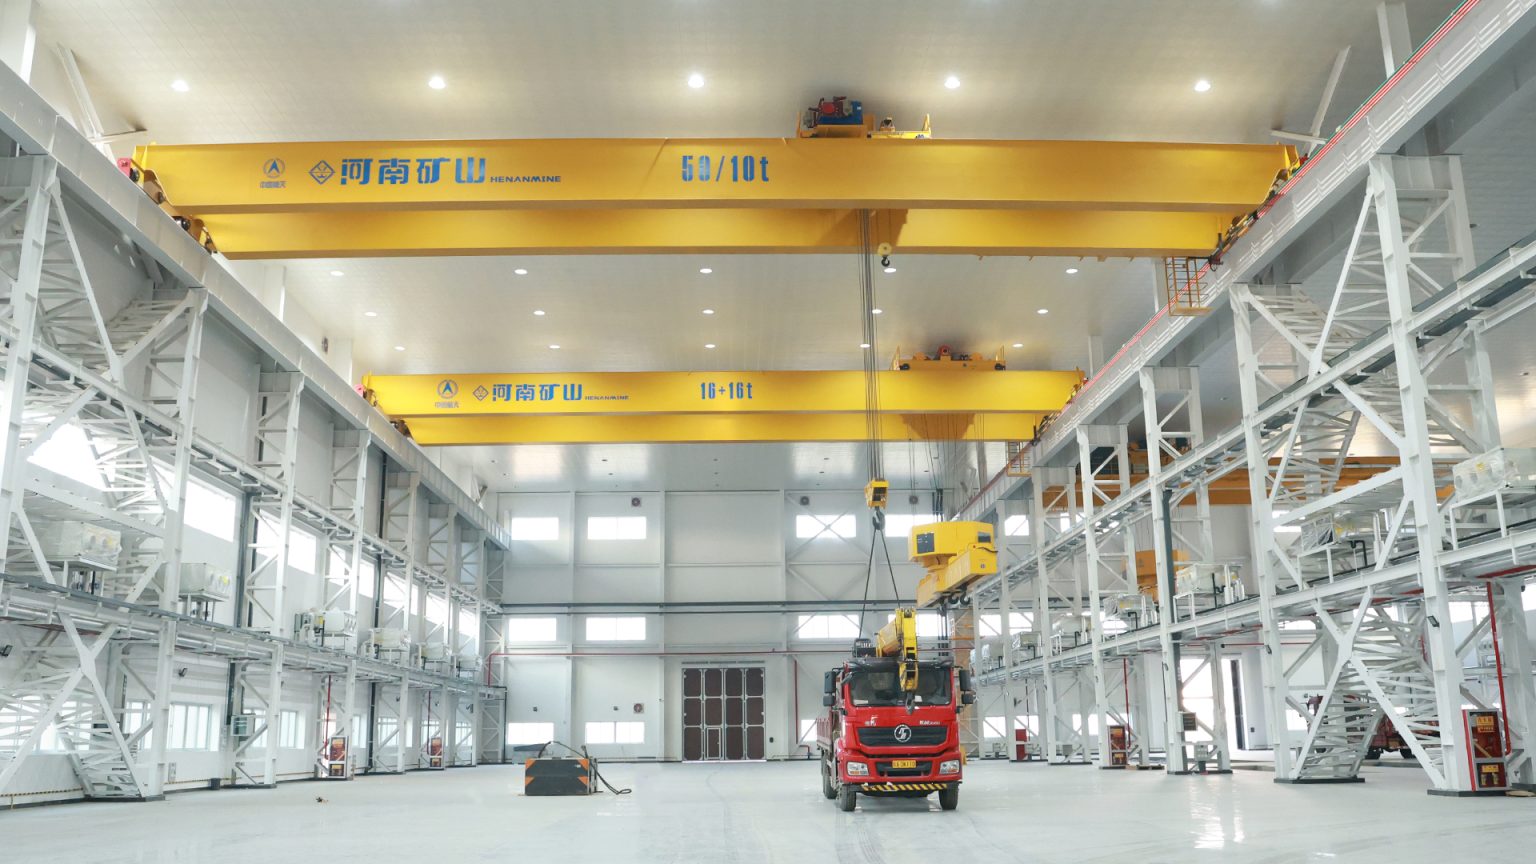
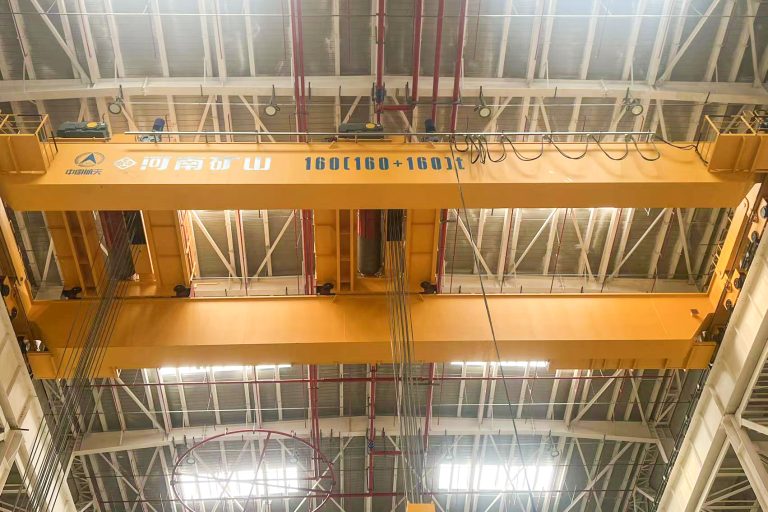
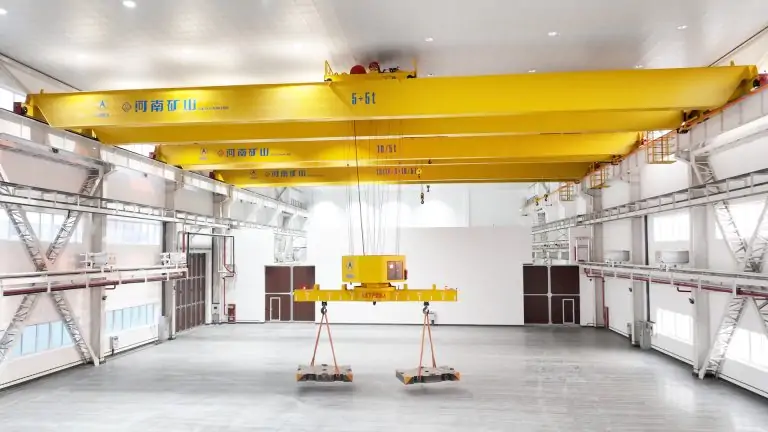
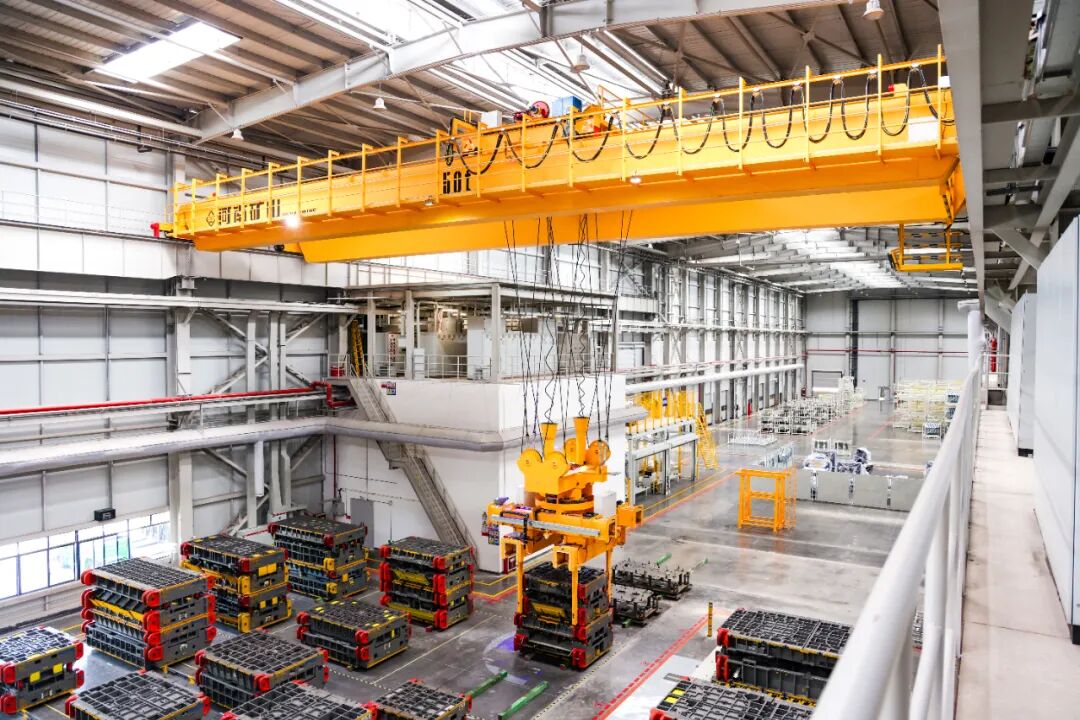
One crane type does not serve every automotive zone. A press shop may require a process-duty double-girder die-handling crane with a dedicated gripper and automatic positioning. A body shop may require an underhung or light workstation system around robots and conveyors. A loading edge or workshop extension may be better served by a semi-gantry crane. Capacity, precision, duty and safety architecture are therefore selected by task rather than by industry name alone.
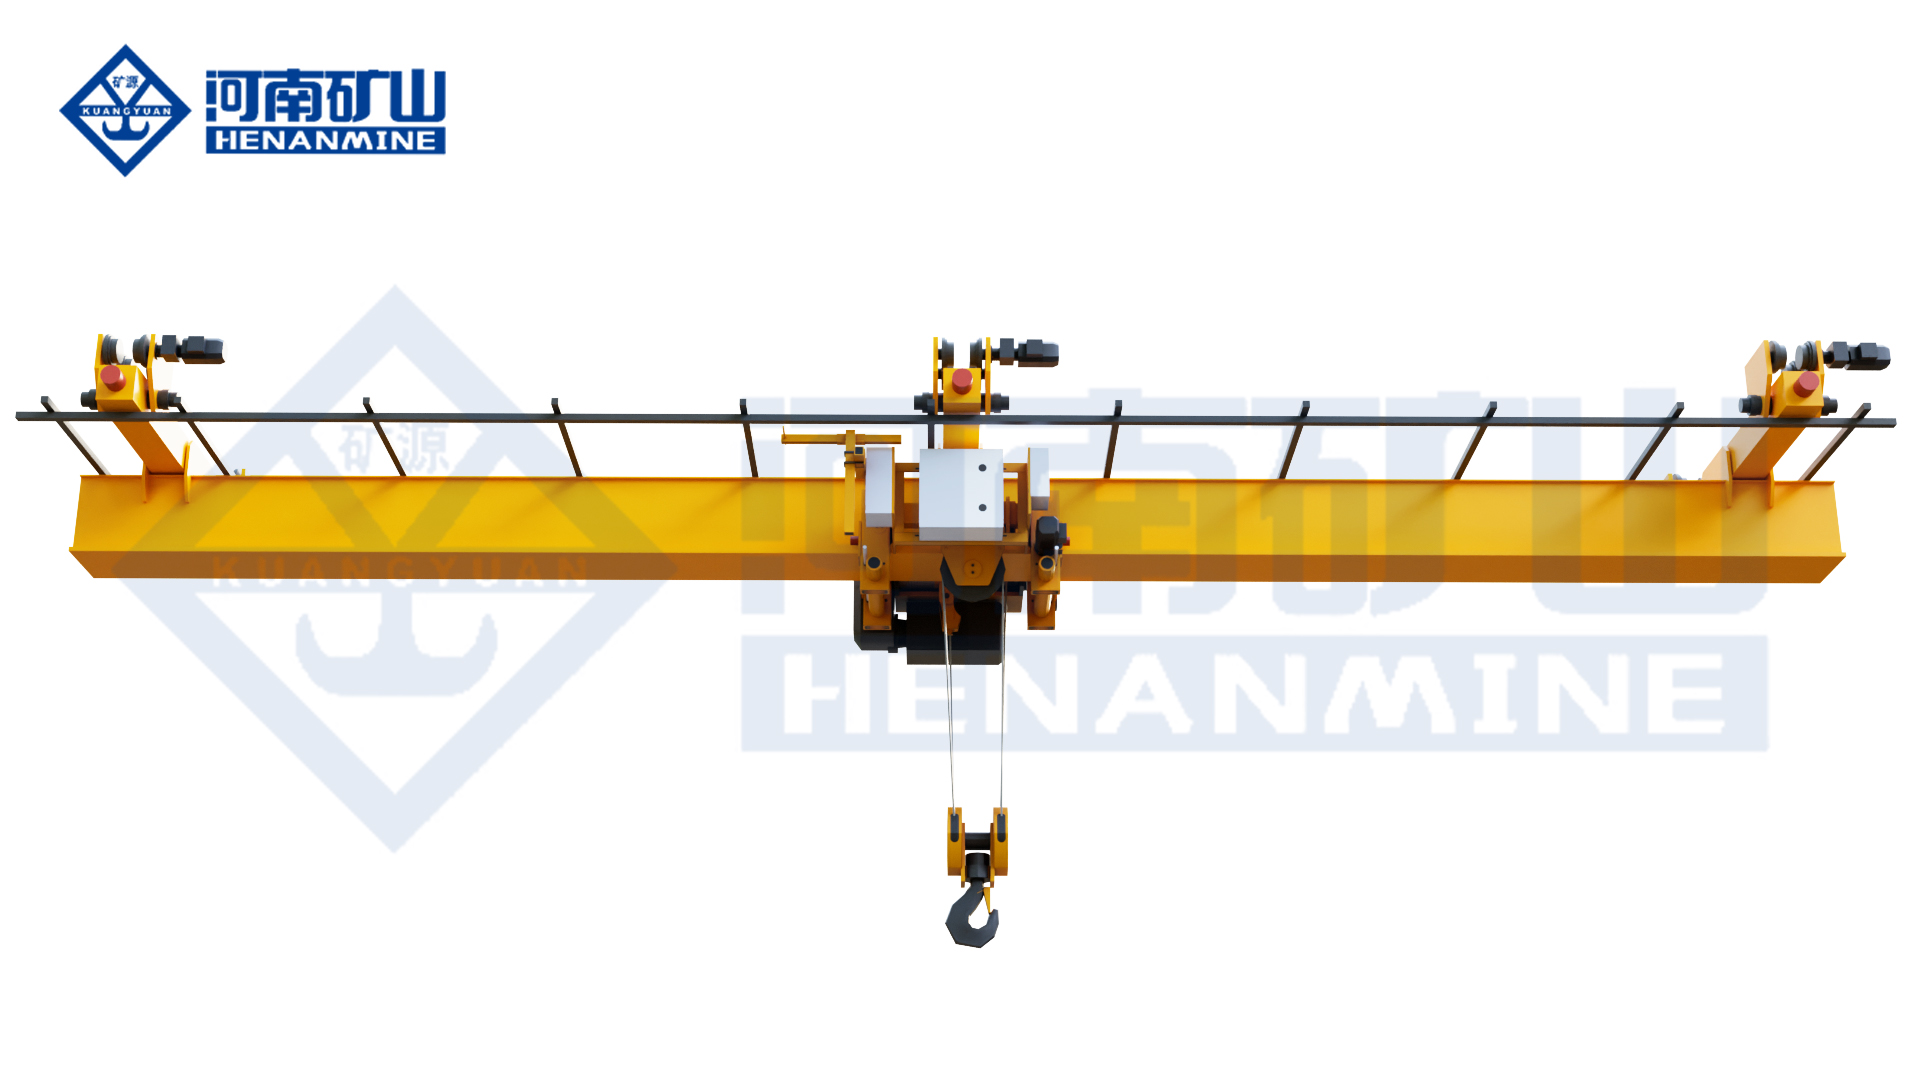
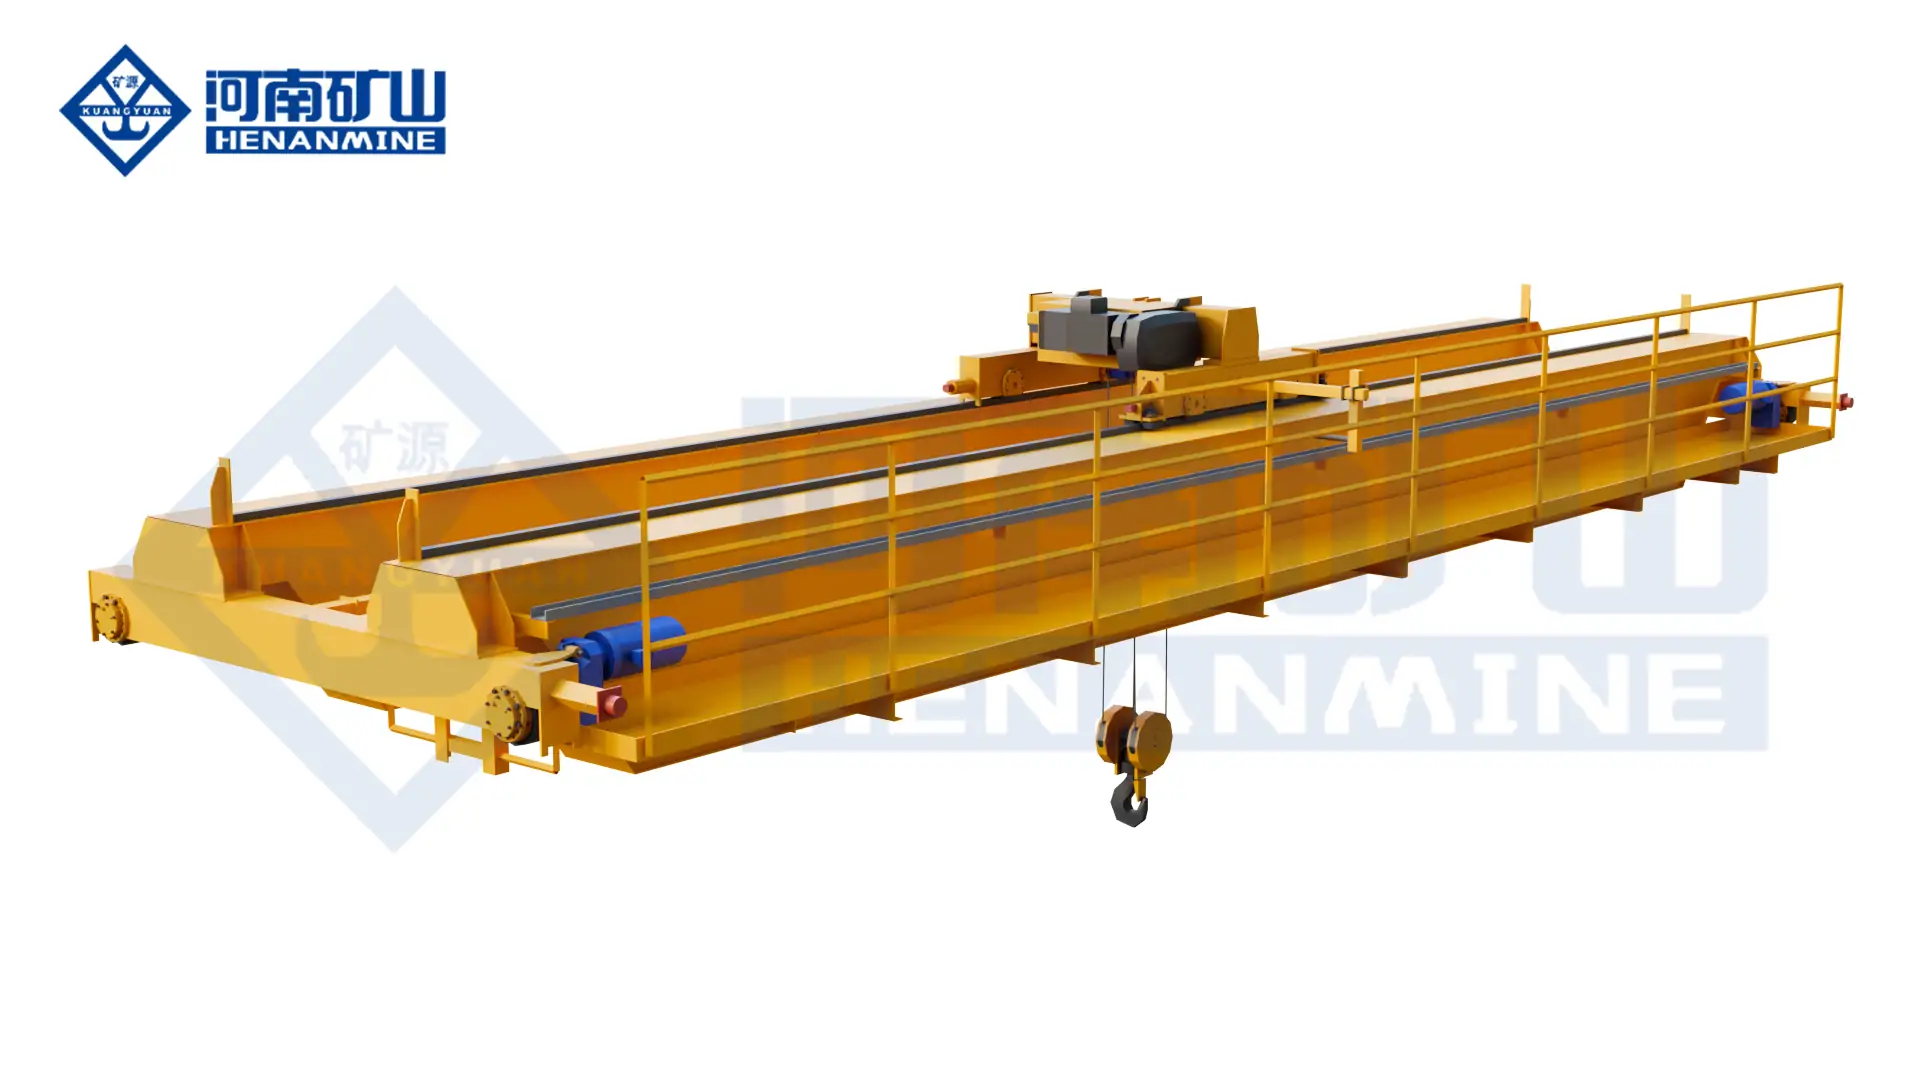
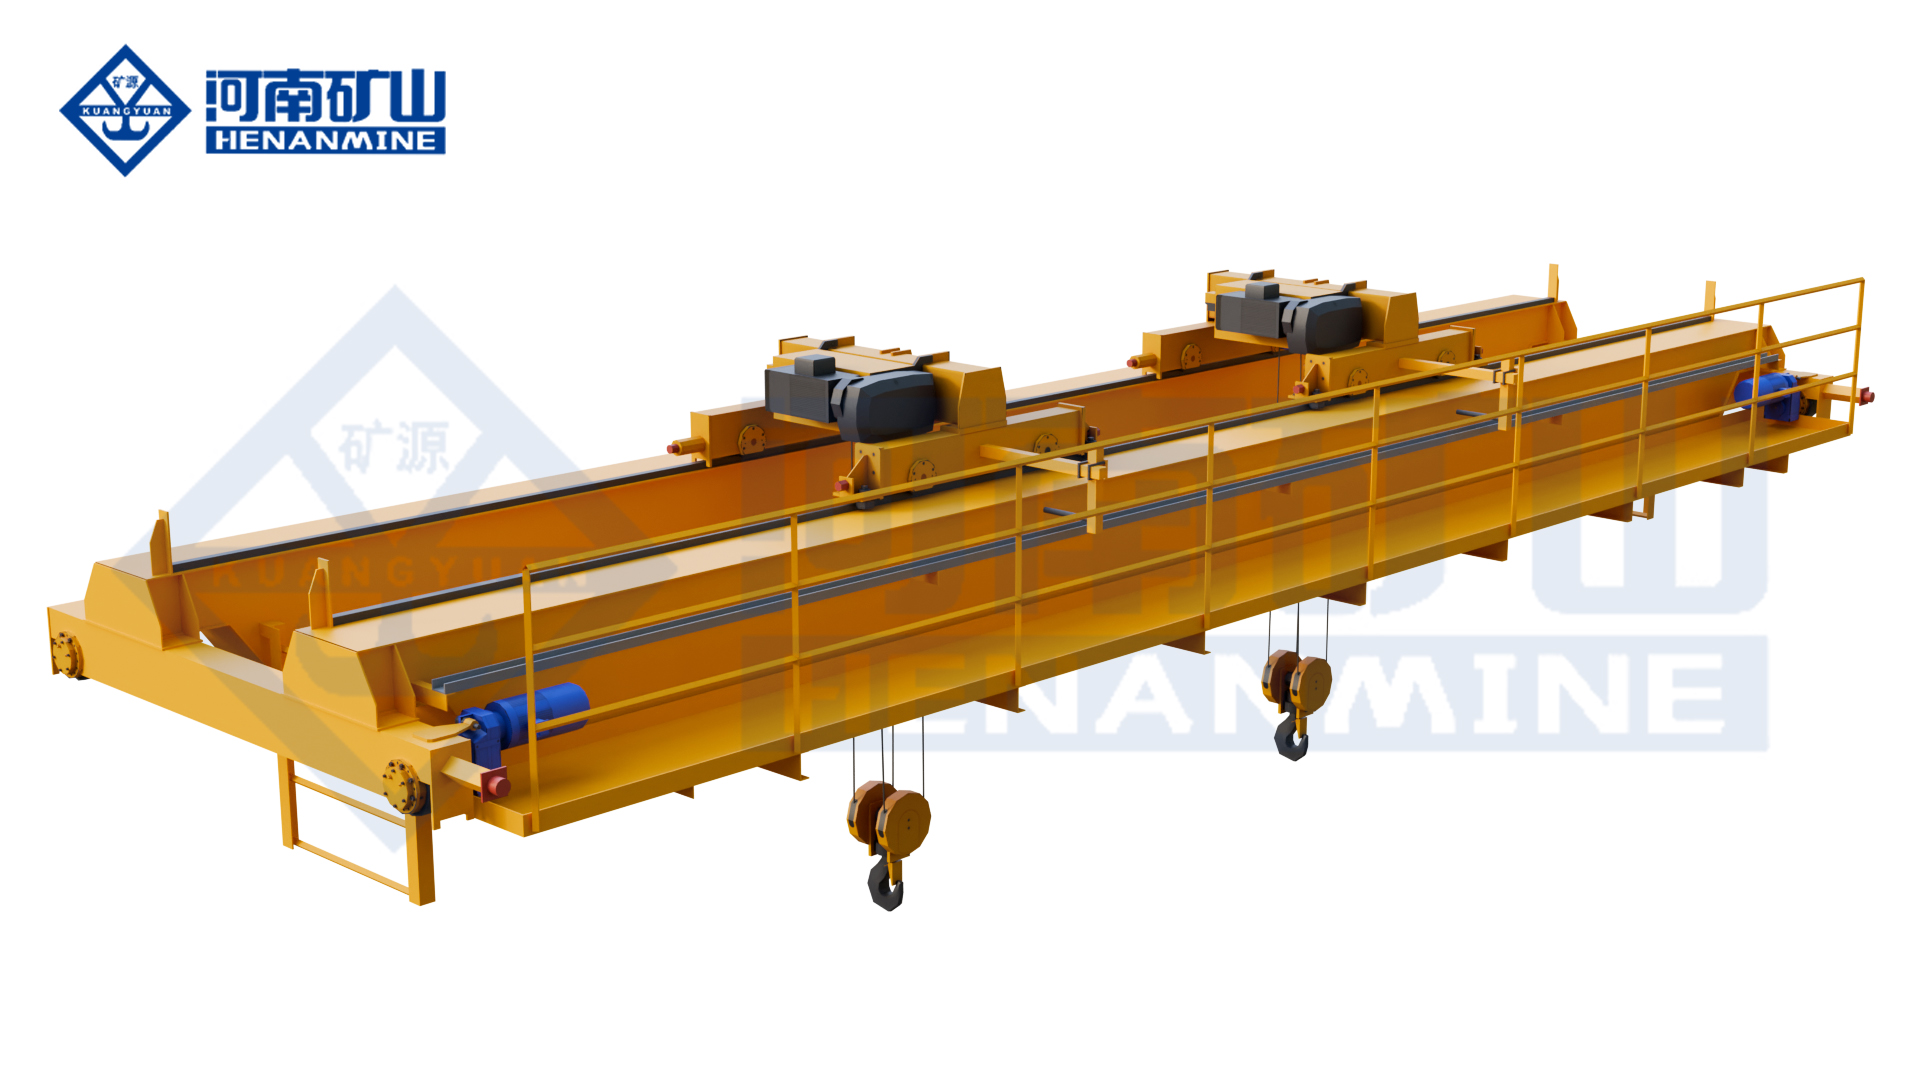
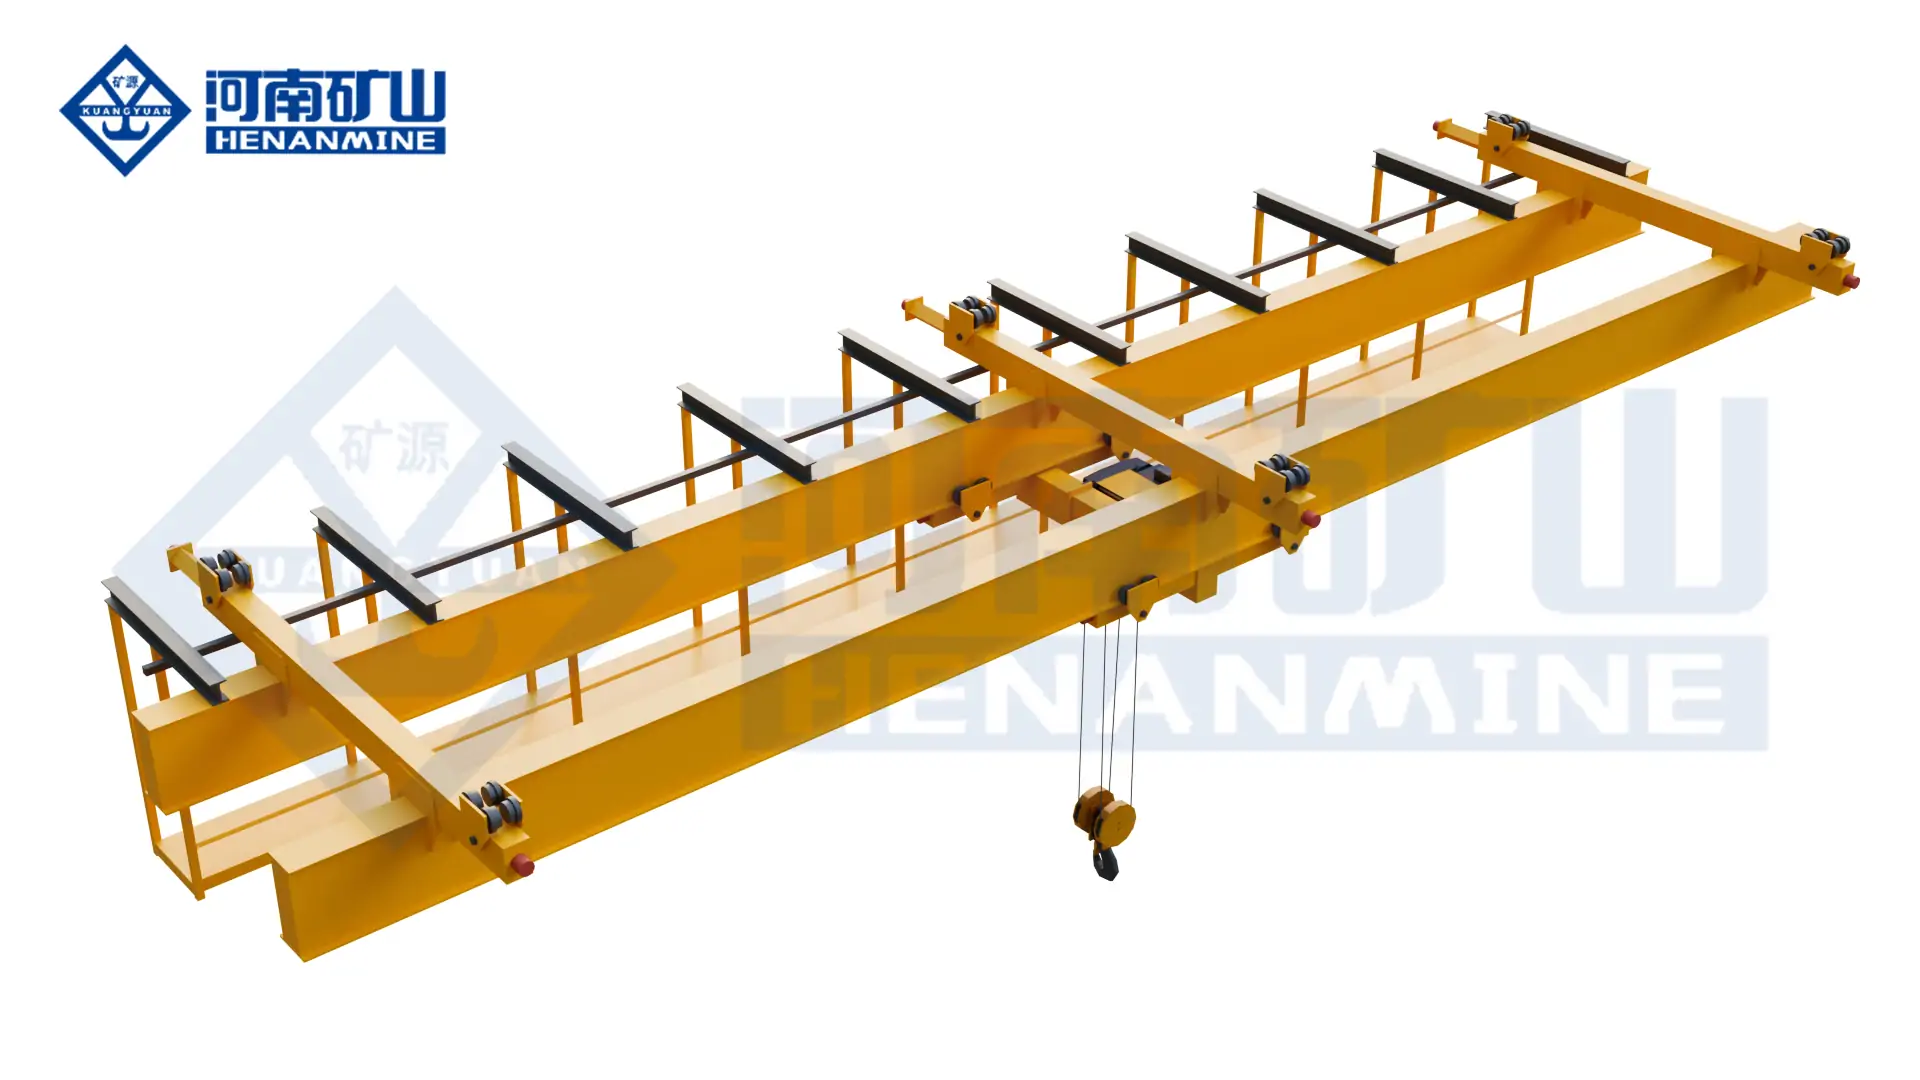
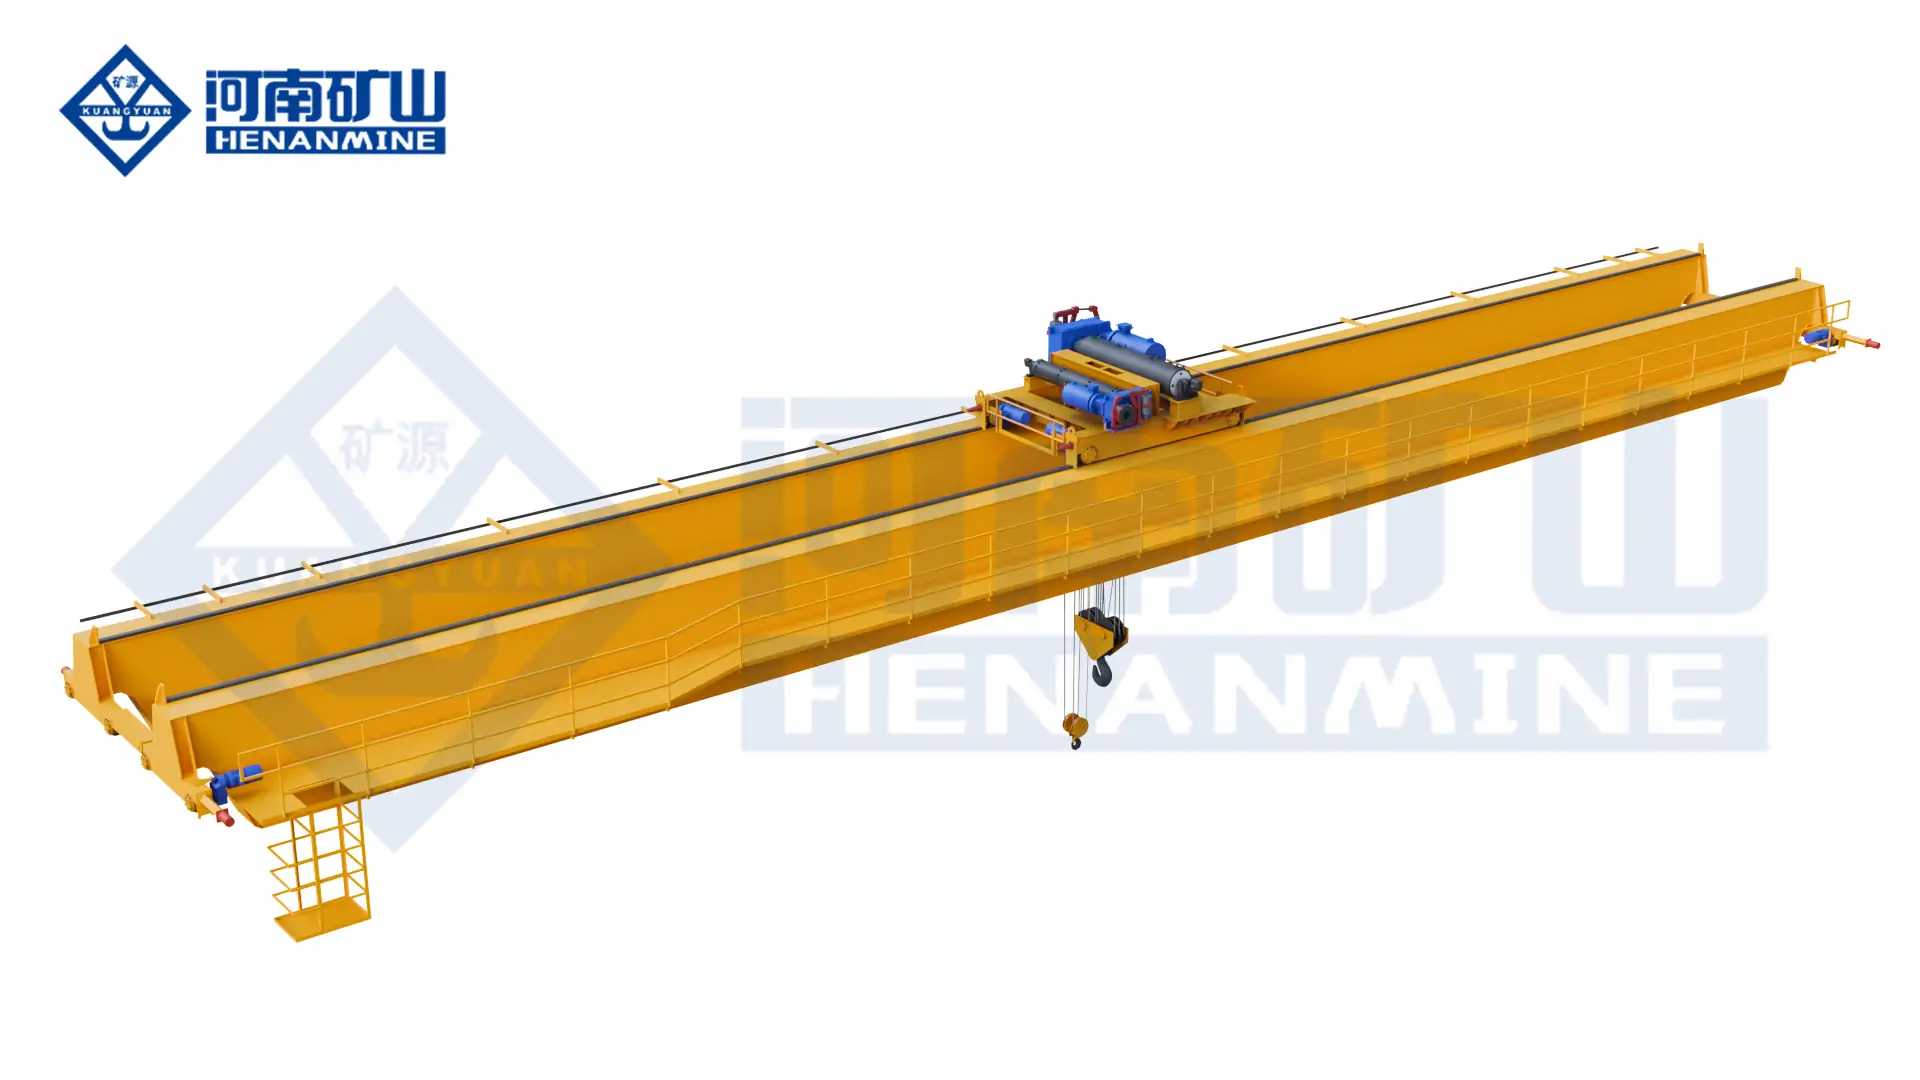
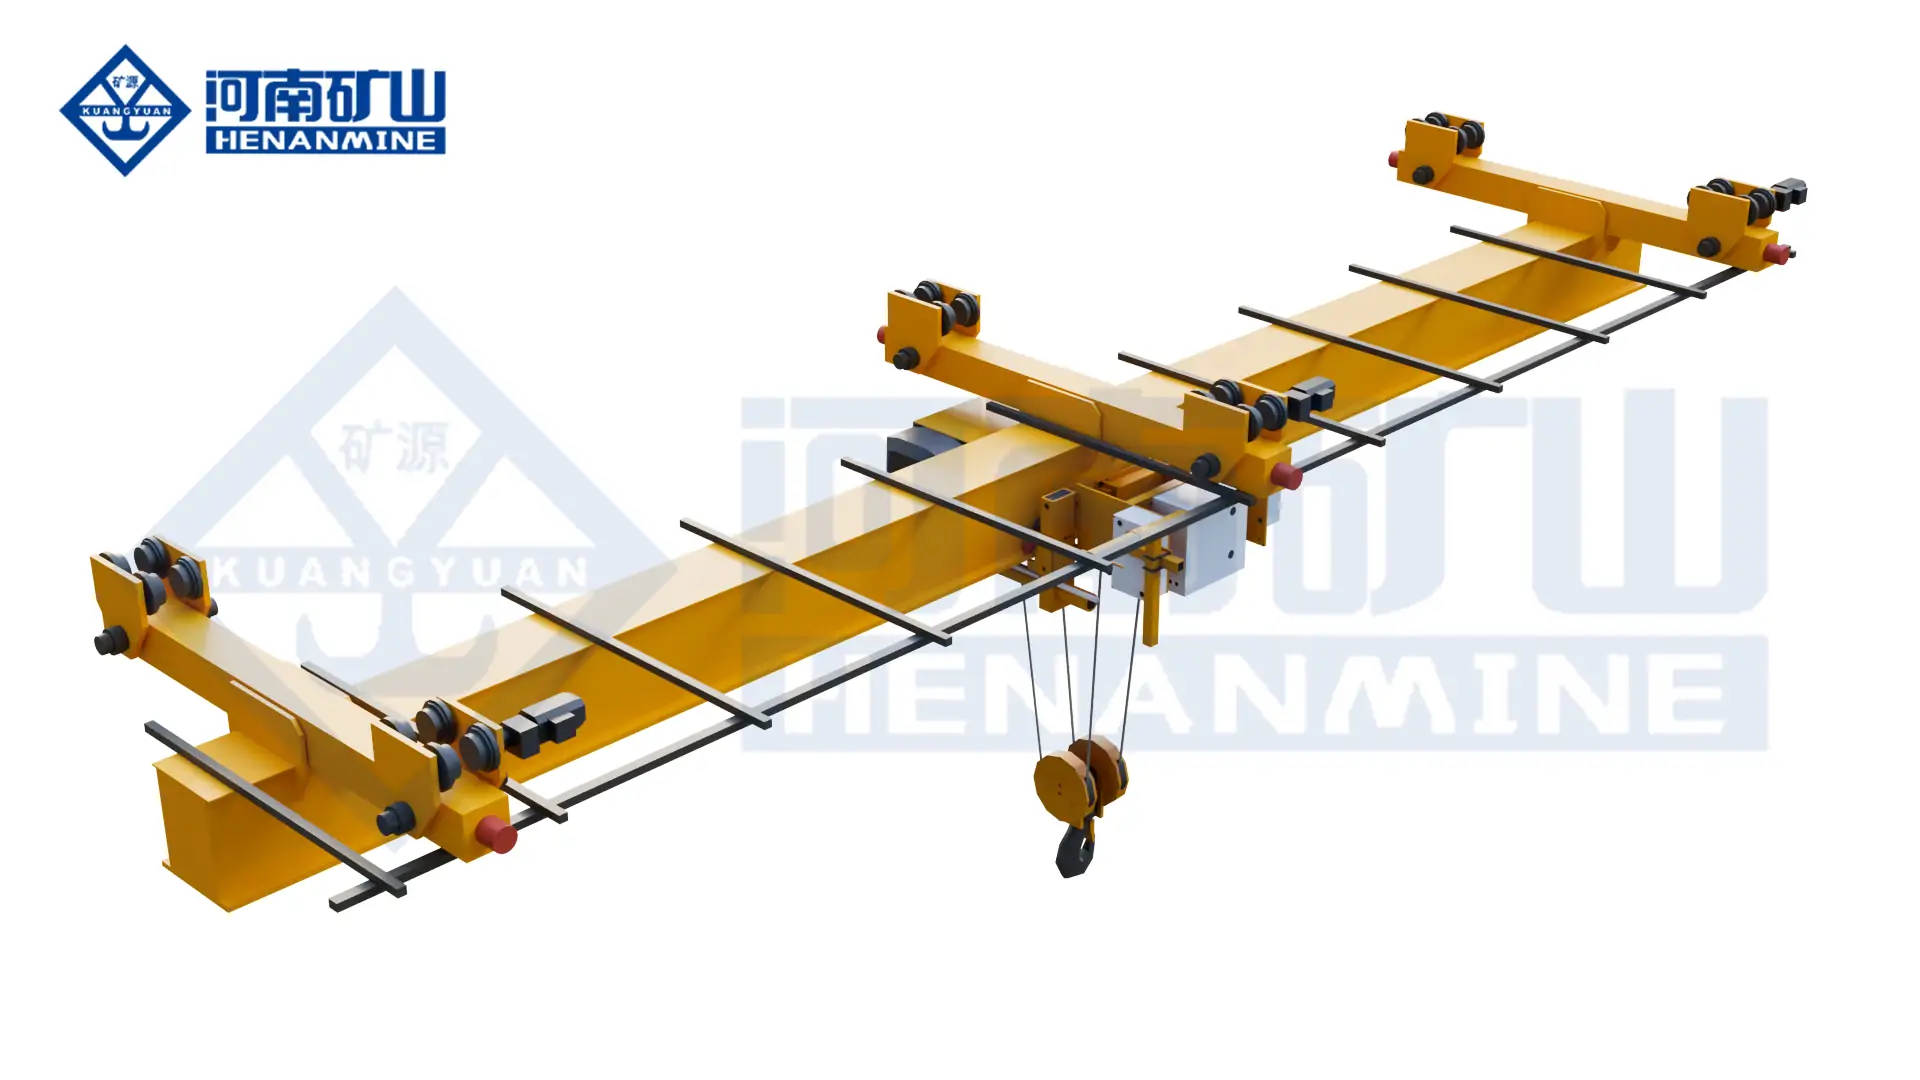
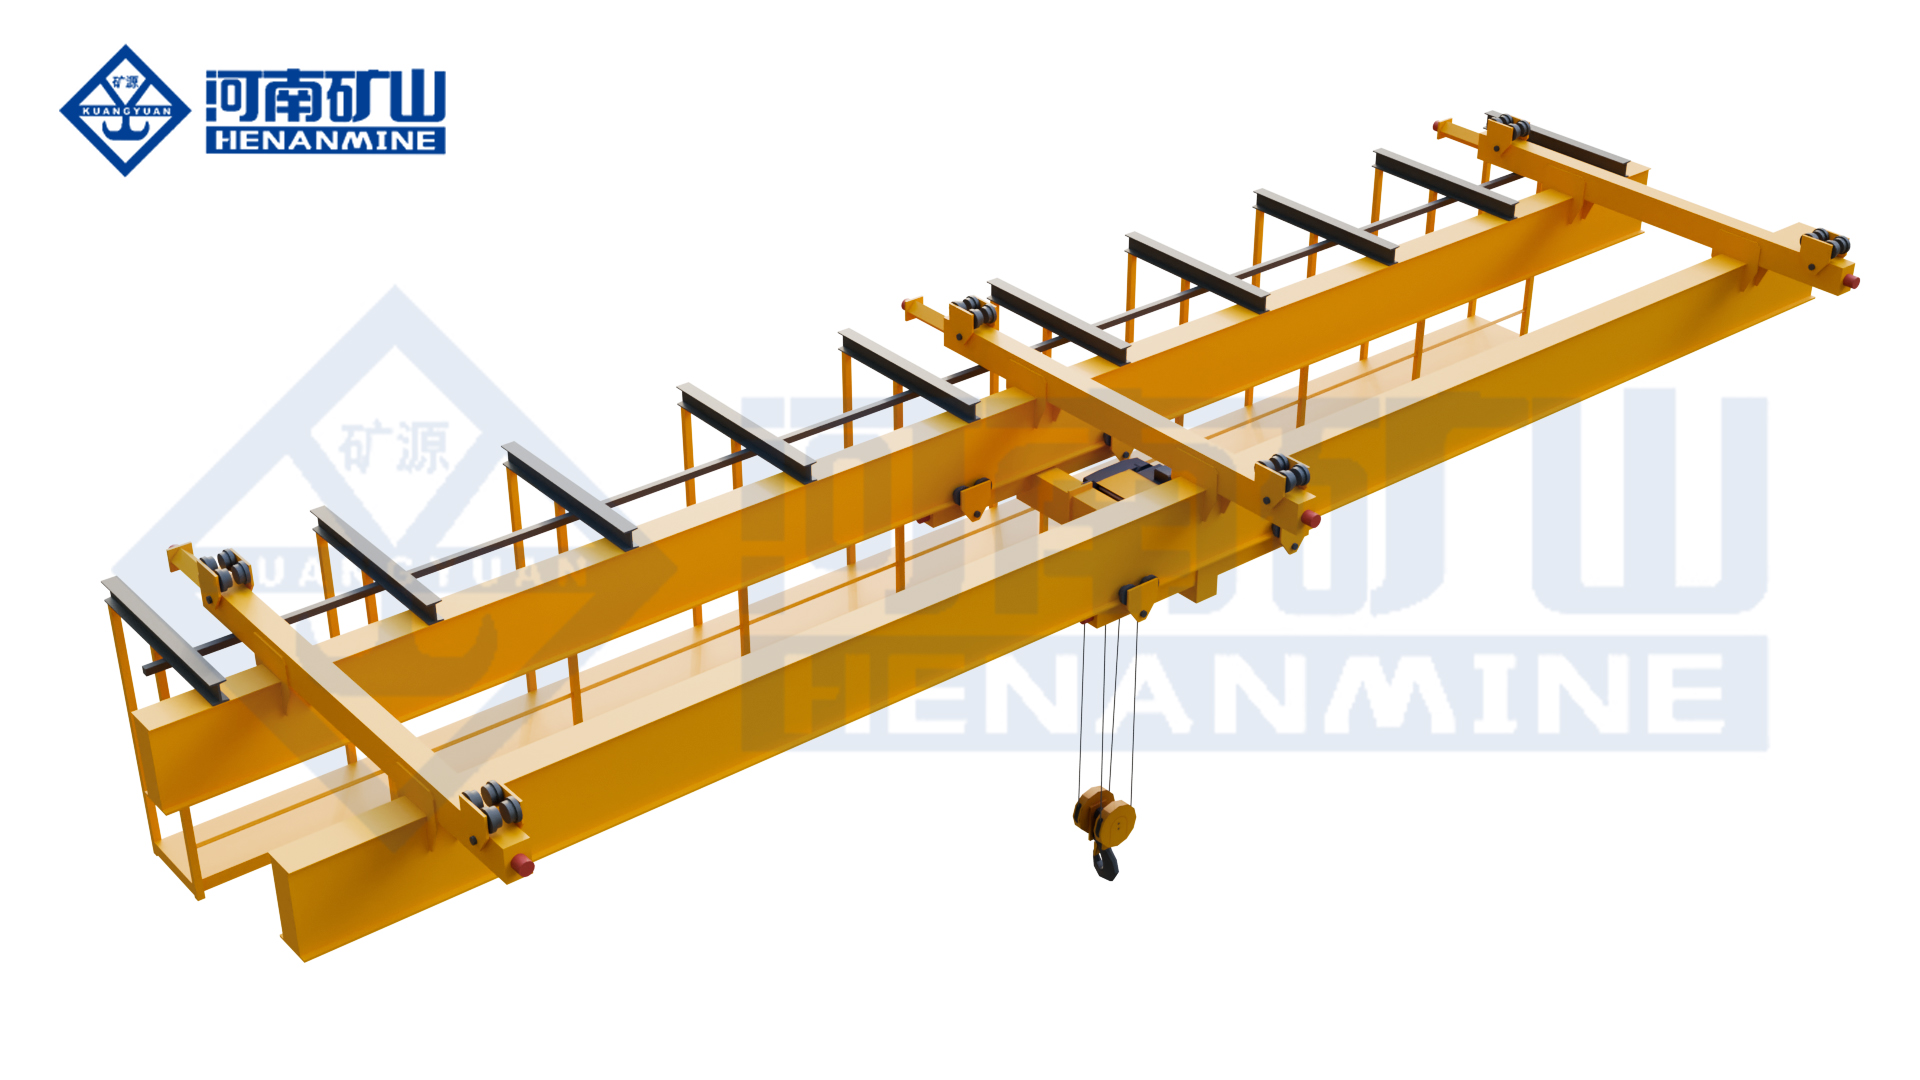
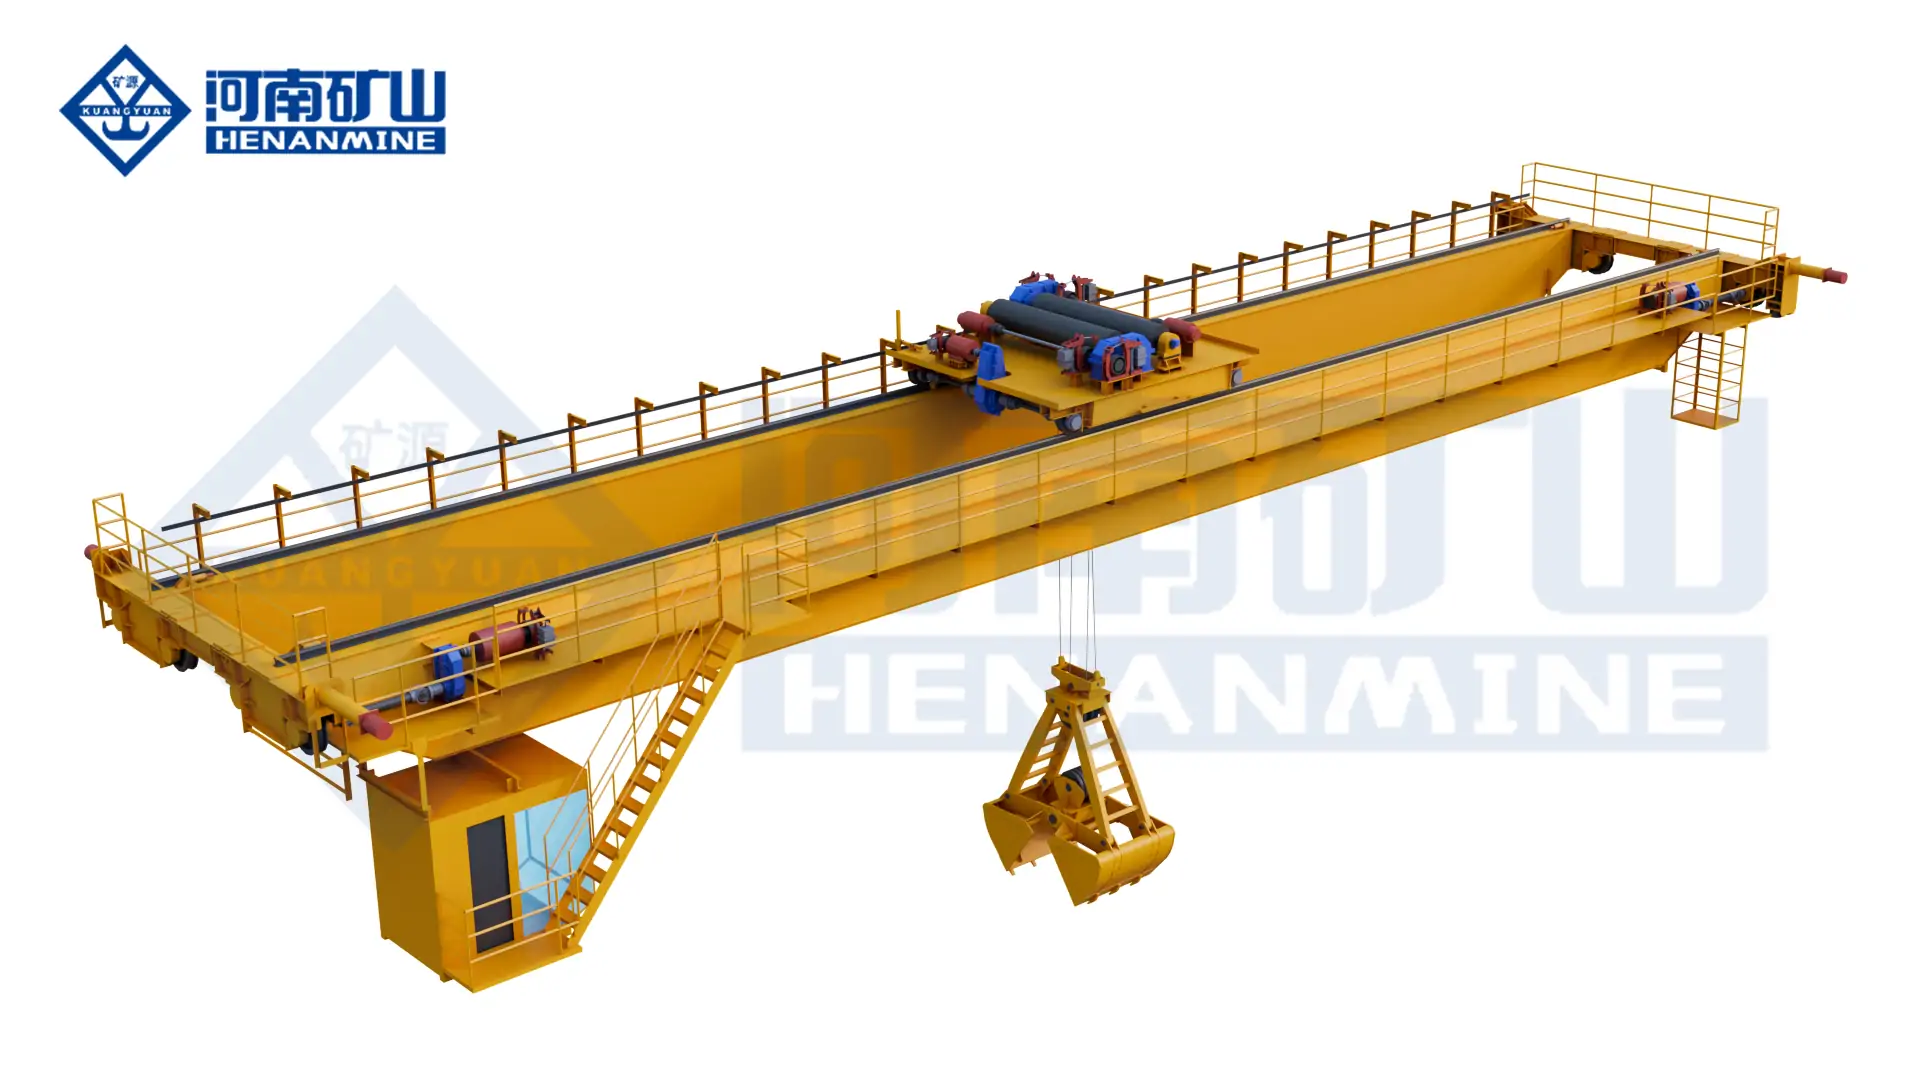
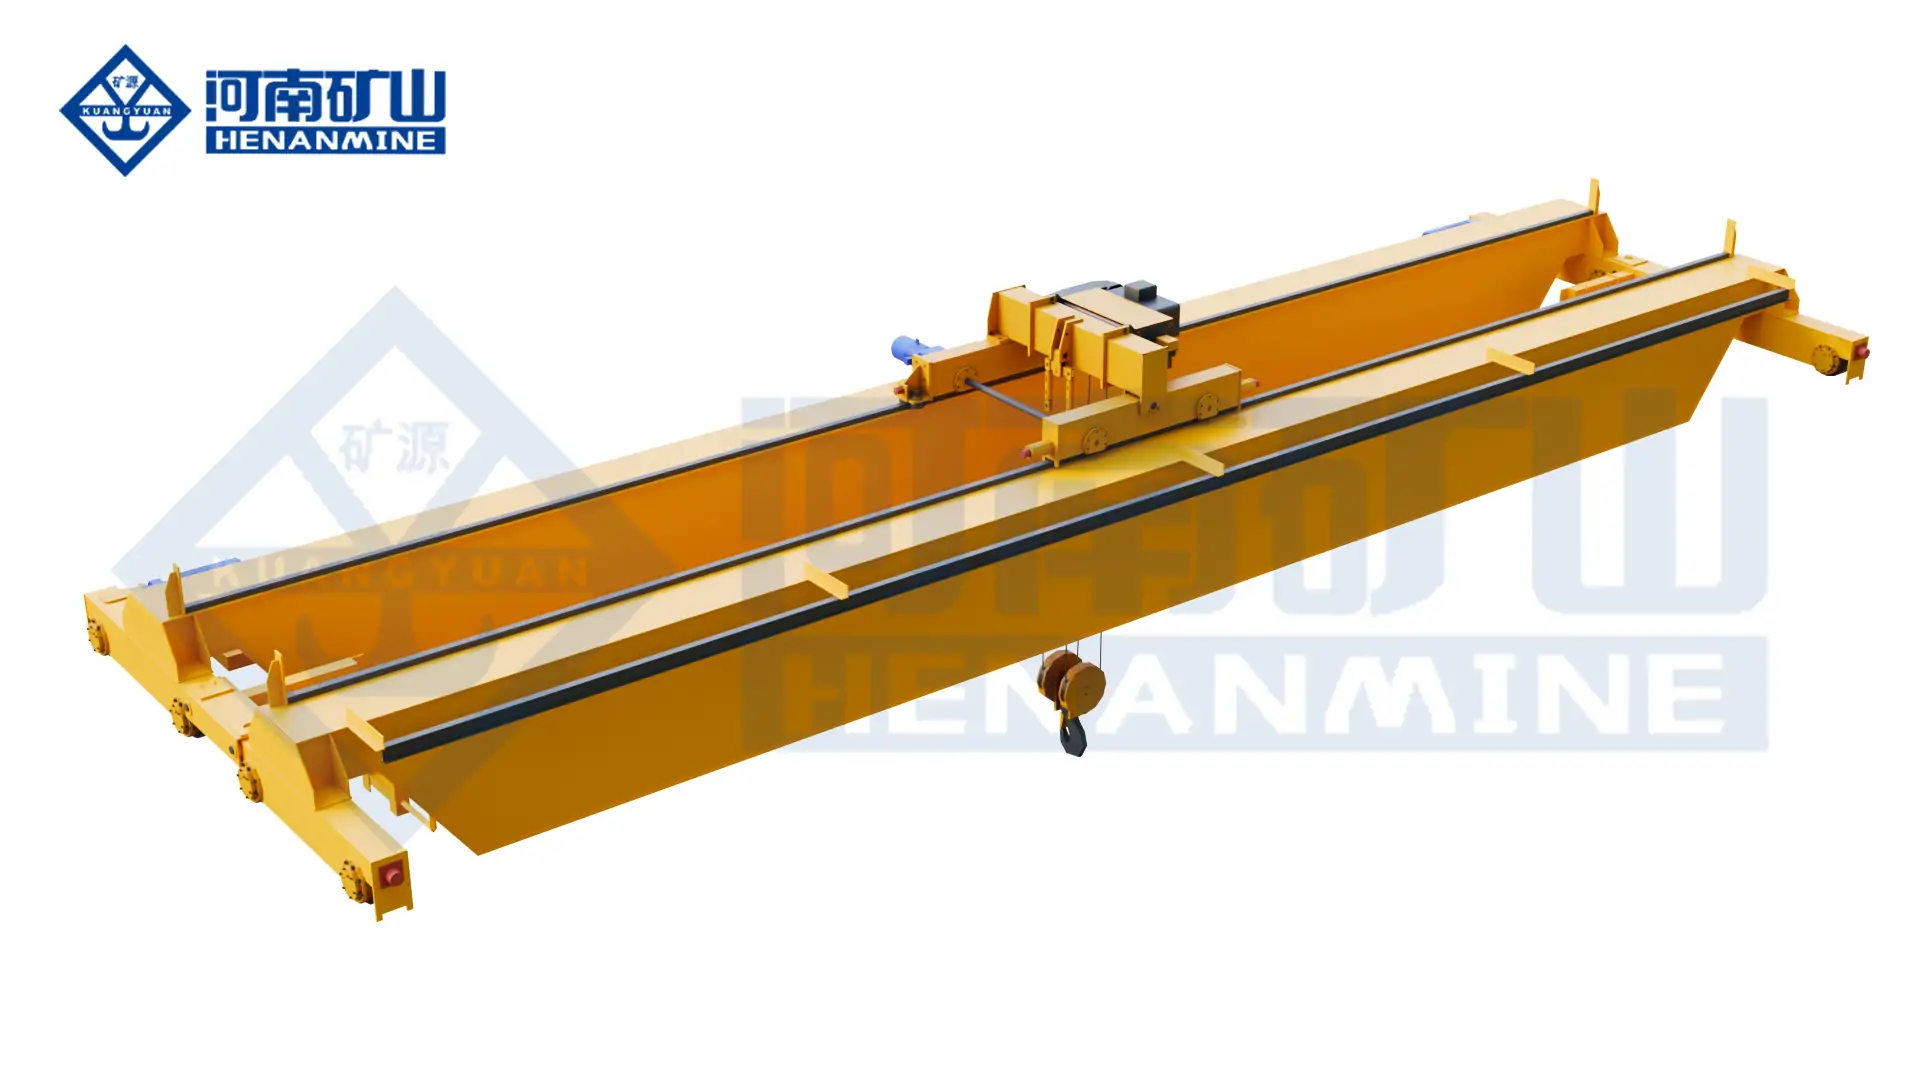
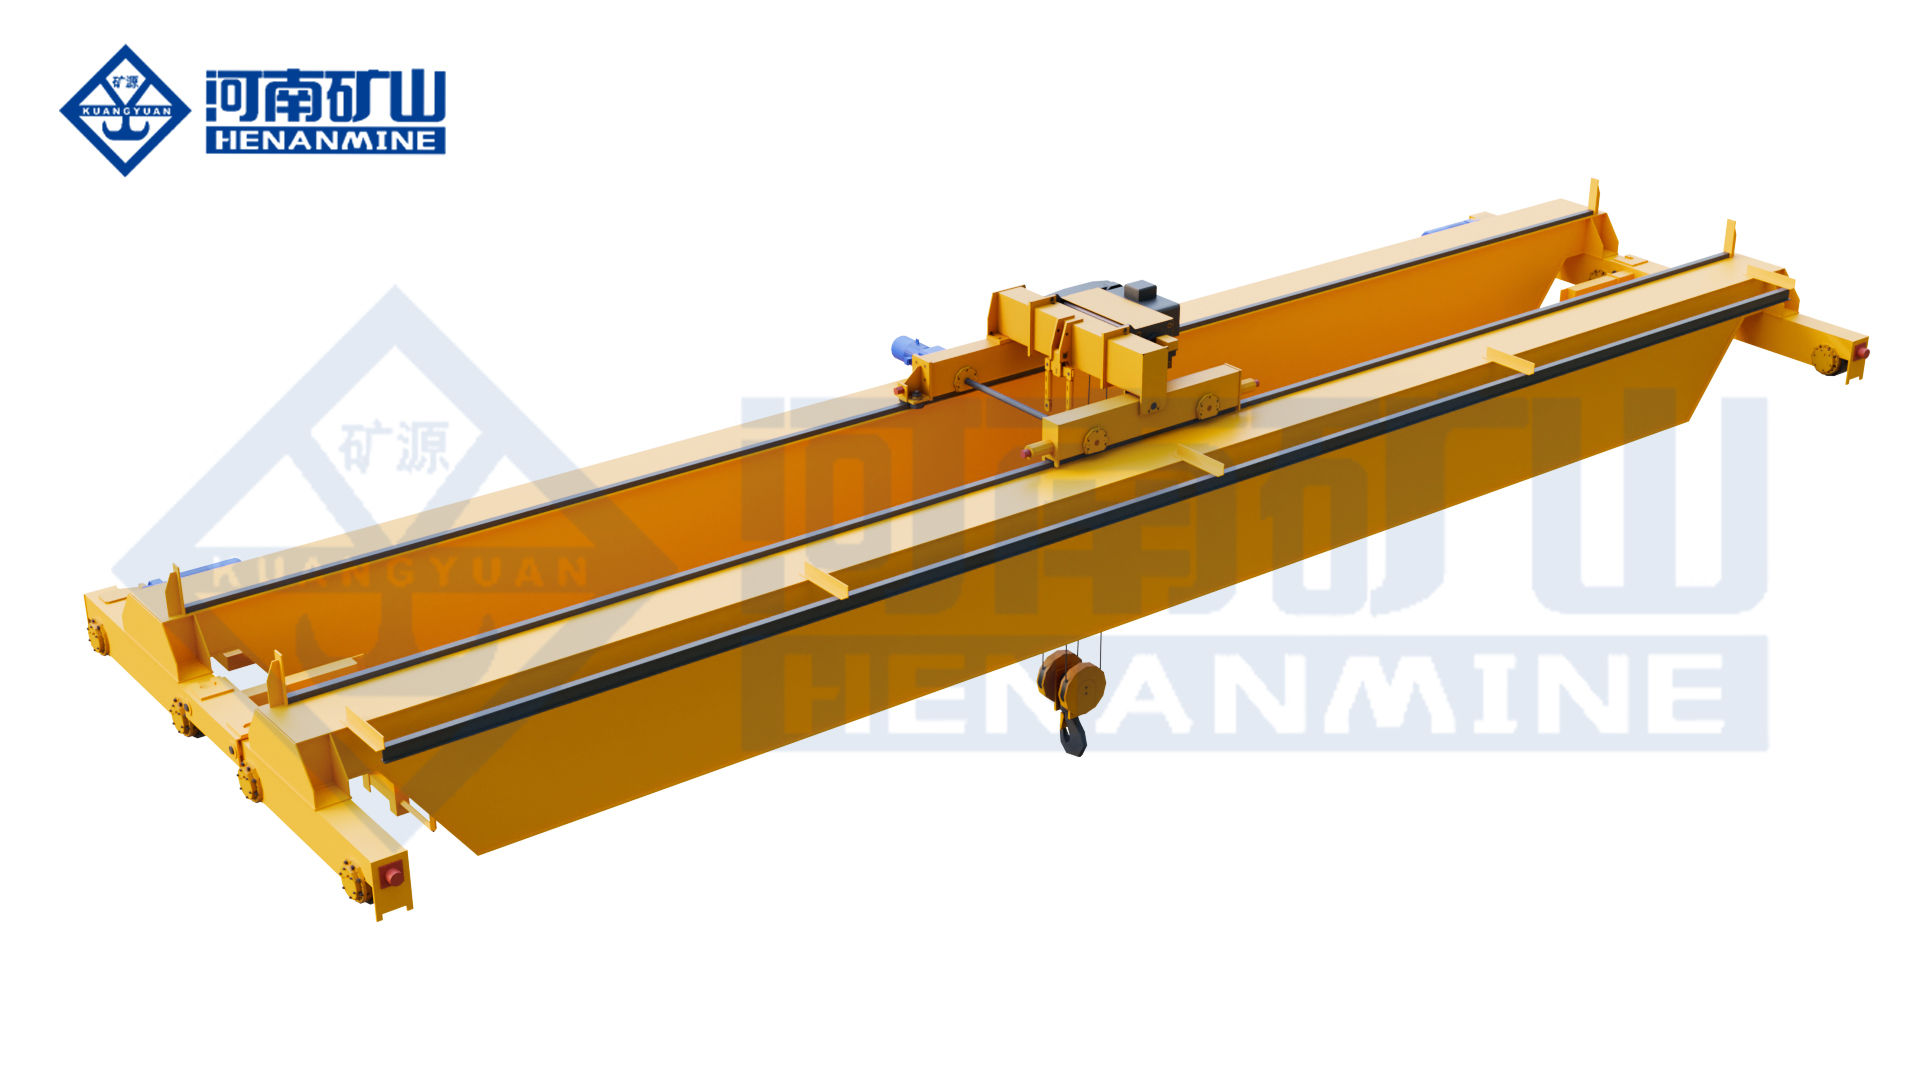
Henan Mine Crane develops automotive lifting solutions from double-girder bridge crane, European-style single-girder crane, single-girder suspension crane and project-specific automated handling platforms.
Automotive Plant Crane Application Map
A plant-wide lifting study records routine production moves, maintenance lifts, emergency recovery tasks and every interface with presses, robots, conveyors, storage systems and vehicle traffic.
1. Coil and Blank Receiving
Unload coils, sheet packs and production materials, then transfer them to storage or blanking lines. Coil orientation, attachment choice, surface protection, aisle clearance and delivery-vehicle exclusion determine the handling concept.
2. Press Shop and Die Store
Retrieve matched die sets, transport them along a protected route and position them at the press or die-change cart. High load, short change windows, offset centers of gravity and controlled seating make this the most demanding automotive crane duty.
3. Body-in-White and Welding
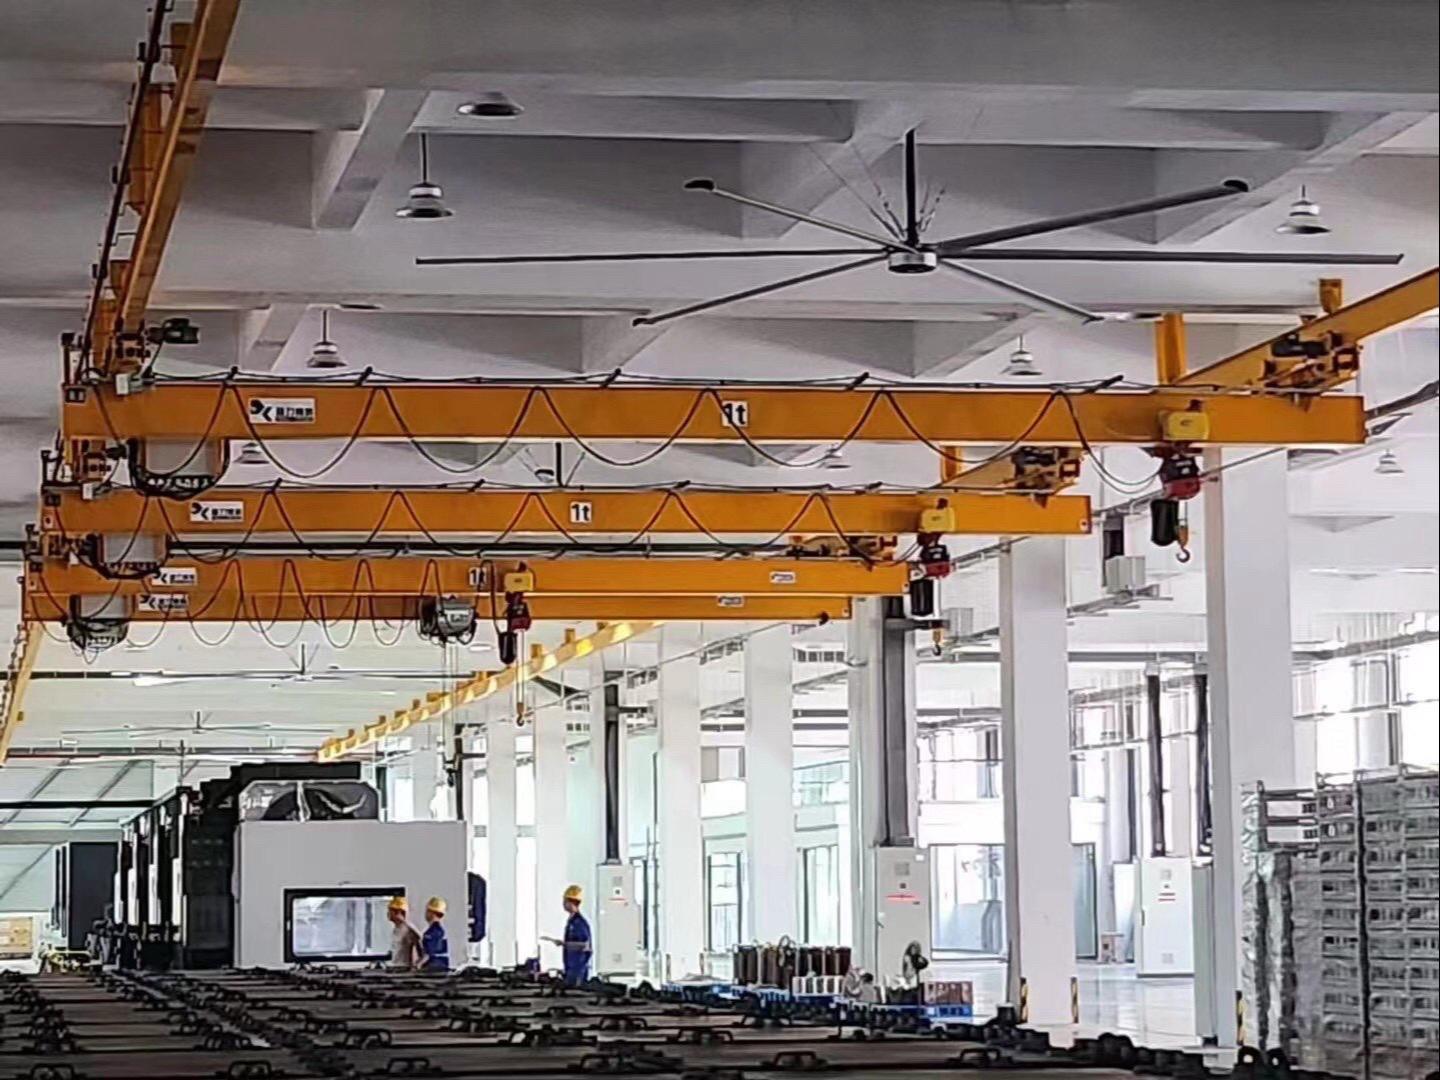
Handle fixtures, welding cells, robots, framing equipment and replacement tooling. Low headroom, crowded services and restricted robot zones often favor underhung, monorail or workstation arrangements.
4. Powertrain and E-Drive
Move engines, transmissions, motors, housings, machining fixtures and test equipment through defined stations. Smooth variable-speed motion, ergonomic controls and application-specific fixtures protect machined surfaces and assembly interfaces.
5. Battery and Paint Areas
Battery-pack assembly, cell production and paint operations have different cleanliness, fire and hazardous-area conditions. The approved environmental and area-classification documents—not the process name—determine enclosure, materials and explosion-protection requirements.
6. General Assembly and Maintenance
Support point-of-use lifting, conveyor work, fixture exchange, line-side replenishment and maintenance shutdowns. Coverage, approach, manual handling risk, parked-load location and unobstructed production flow shape the layout.
Automotive Industry Crane System Architecture
Bridge and Runway
Single- or double-girder, top-running or underhung architecture is selected from capacity, span, headroom, approach, building reactions, process coverage and required stiffness.
Hoisting Machinery
Wire-rope hoist or open-winch machinery is sized from gross load, lift, speeds, starts, load spectrum, precision, brake strategy and required production availability.
Die or Component Attachment
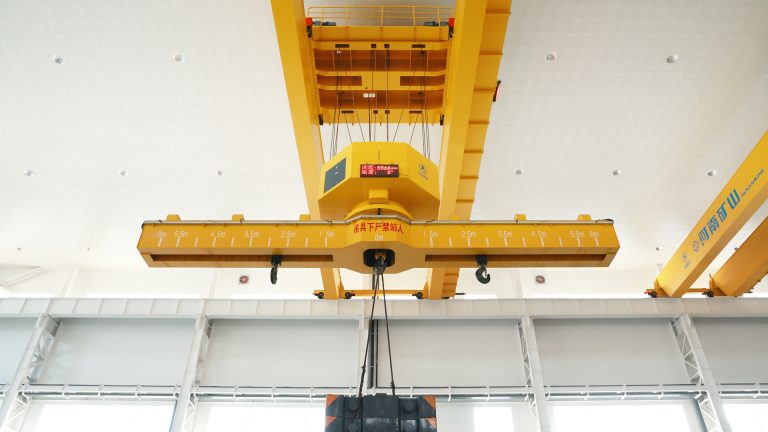
A die gripper, lifting beam, tong, C-hook, vacuum device, manipulator or certified hook rigging engages the declared load family and includes positive confirmation where the risk assessment requires it.
Motion and Positioning
Variable-frequency drives, controlled acceleration, creep speed, encoders, load-height feedback and anti-sway functions support stable travel and repeatable final approach.
Controls and Plant Interface
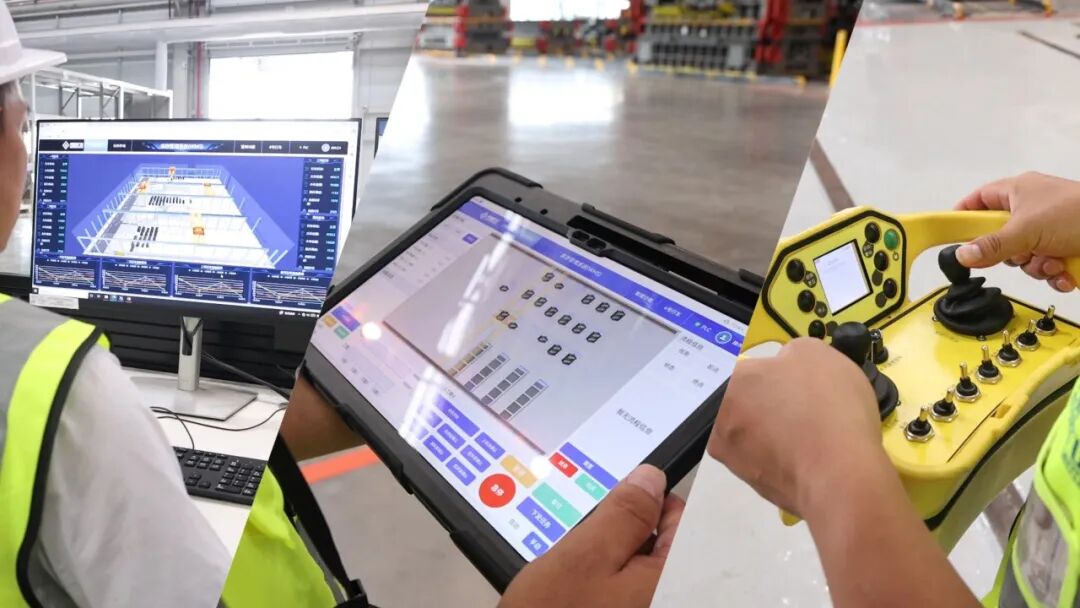
Pendant, radio, cabin or remote-control-room operation can integrate with press controls, WCS, MES, storage management, access gates and maintenance authorization.
Inspection and Recovery Access
Walkways, platforms, isolation stations, attachment stands, rescue provisions and component-removal paths are coordinated with production equipment before fabrication.
Automotive Industry Crane Selection Considerations
Rated tonnage is only one selection input. The complete load envelope, process sequence and consequence of delayed changeover define the appropriate crane.
Load Family and Center of Gravity
Maximum and minimum mass, dimensions, lifting points, center-of-gravity range, surface restrictions and orientation are documented for every die, fixture, component and maintenance load.
Cycle and Availability
Die changes per shift, travel path, storage retrieval, press occupancy, average load, starts per hour, annual operating hours and recovery strategy determine mechanism duty and redundancy.
Placement and Approach
Required coordinates, allowable approach, final speed, die-cart interface, rack geometry, press centerline and permissible alignment error are specified as measurable acceptance values.
Building and Process Envelope
Runway elevation, roof, columns, presses, racks, robots, conveyors, utilities, access doors and neighboring cranes are checked in a coordinated three-dimensional clearance model.
Control and Data Scope
Manual, assisted or automatic operation; die identification; task source; station handshakes; protected areas; event records; cybersecurity and manual recovery are defined before controls are priced.
Environment and Maintenance
Press-shop vibration, lubricants, welding fumes, dust, heat, washdown, paint solvents, dry-room conditions and scheduled shutdown windows establish the protection and service concept.
Automotive Industry Crane Configurations Compared
| Configuration | Typical Automotive Duty | Principal Strength | Critical Engineering Check |
|---|---|---|---|
| Automated Die-Handling Process Crane | Die store retrieval, press feeding and return | Repeatable high-load transfer with dedicated attachment and plant integration | Die database, grip confirmation, center of gravity, positioning, protected route and safe recovery |
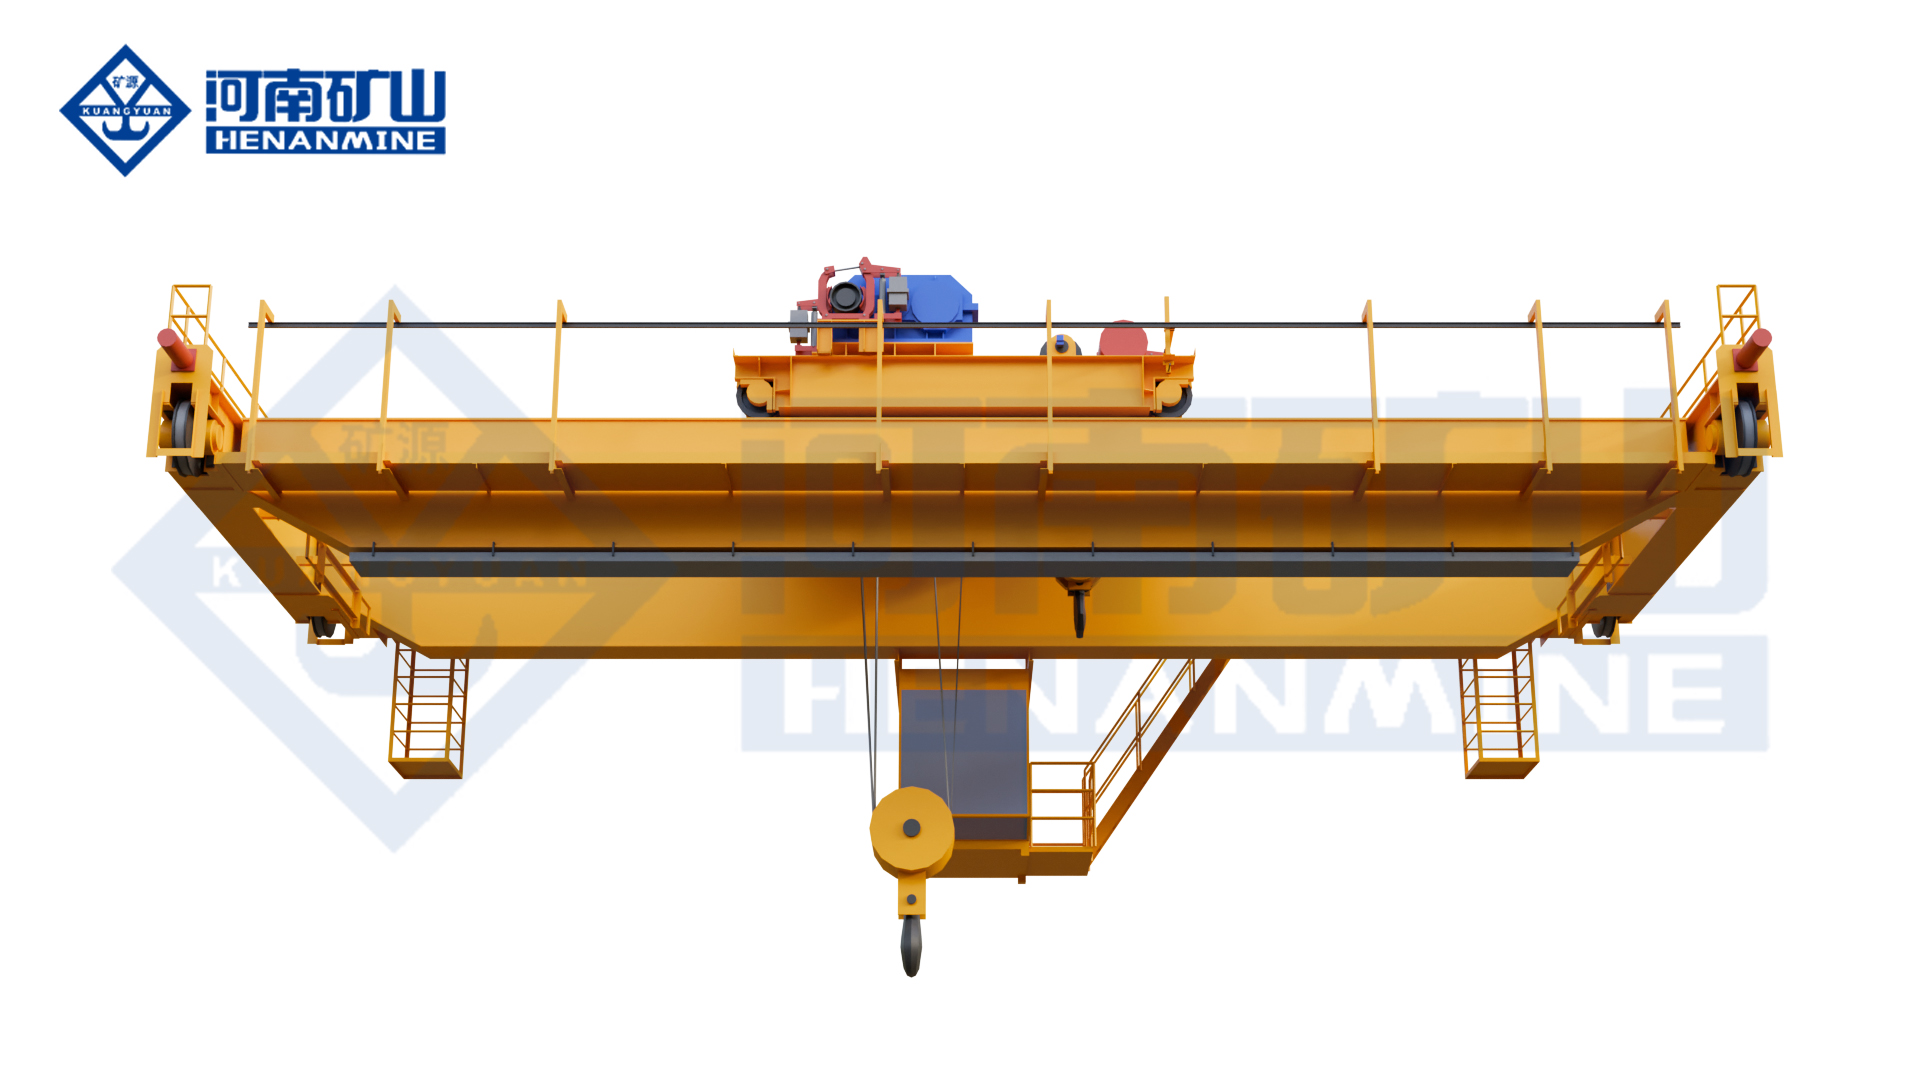
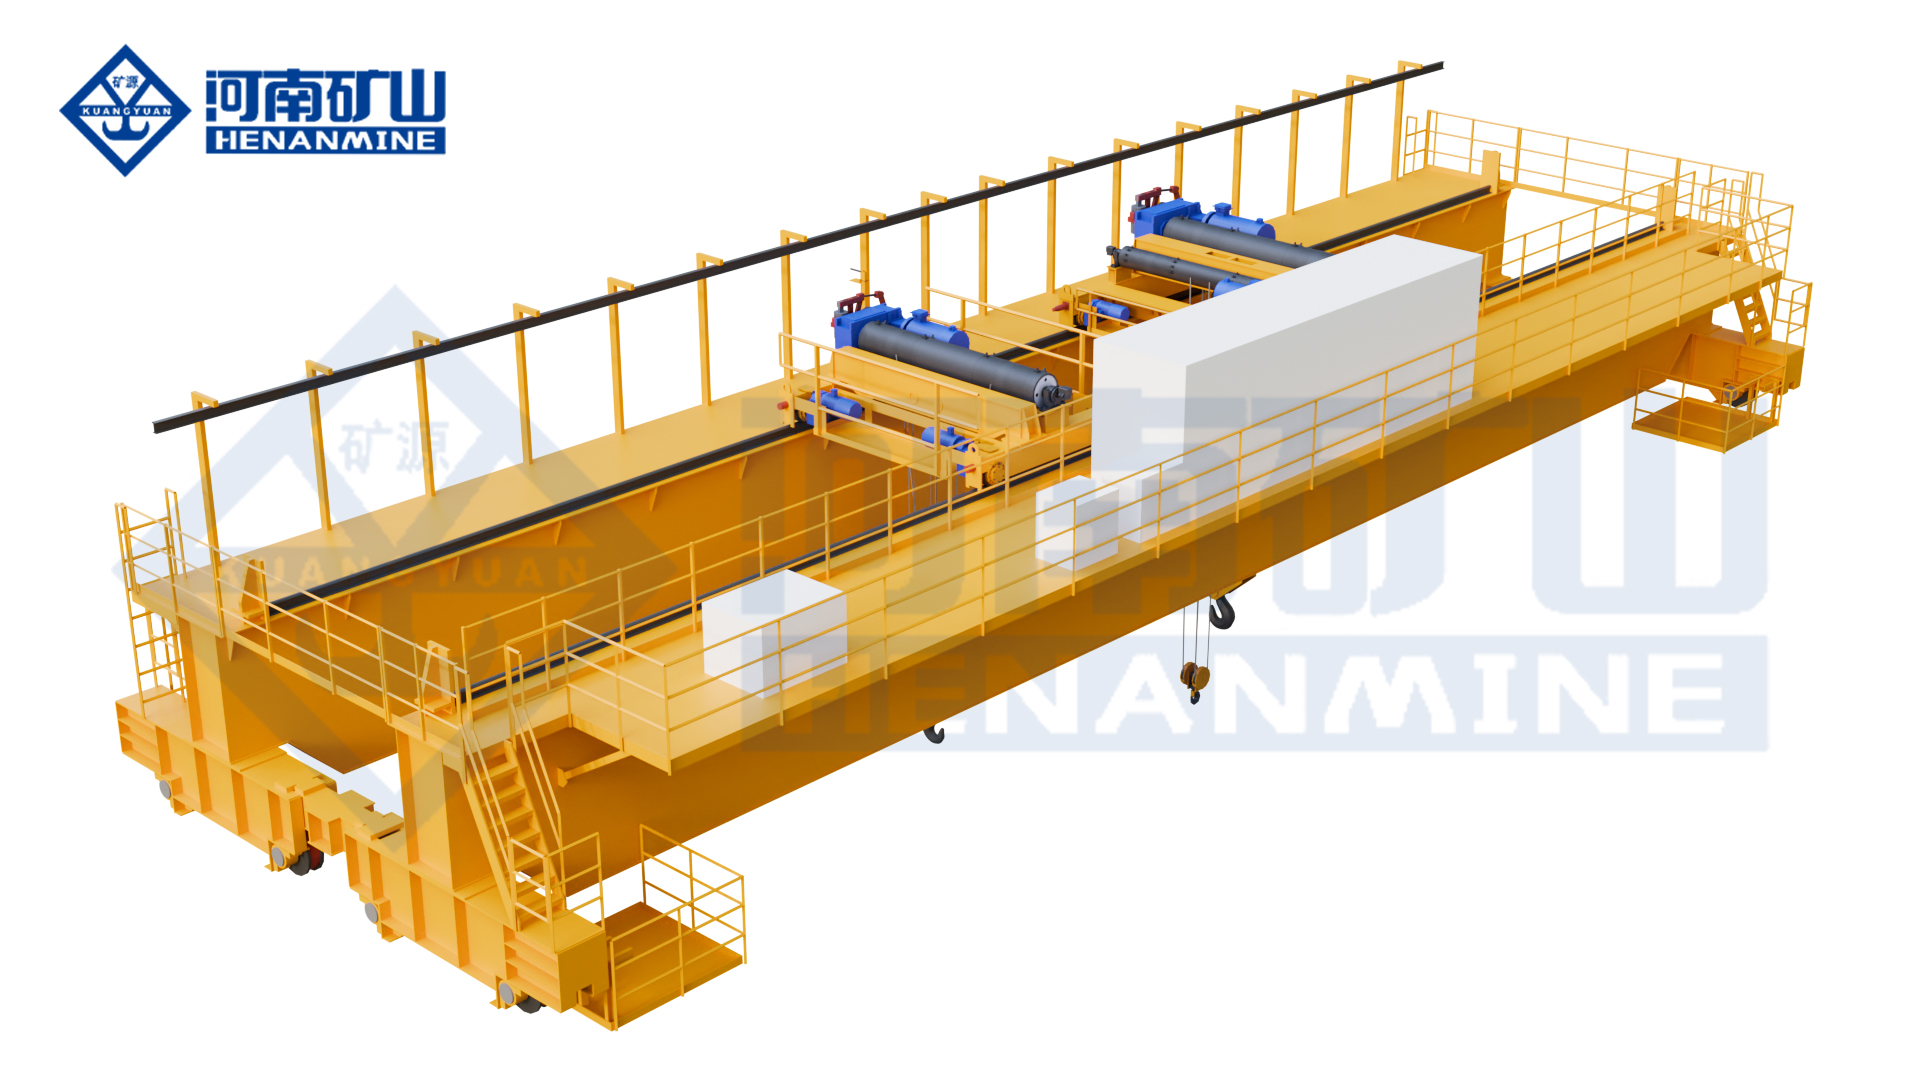
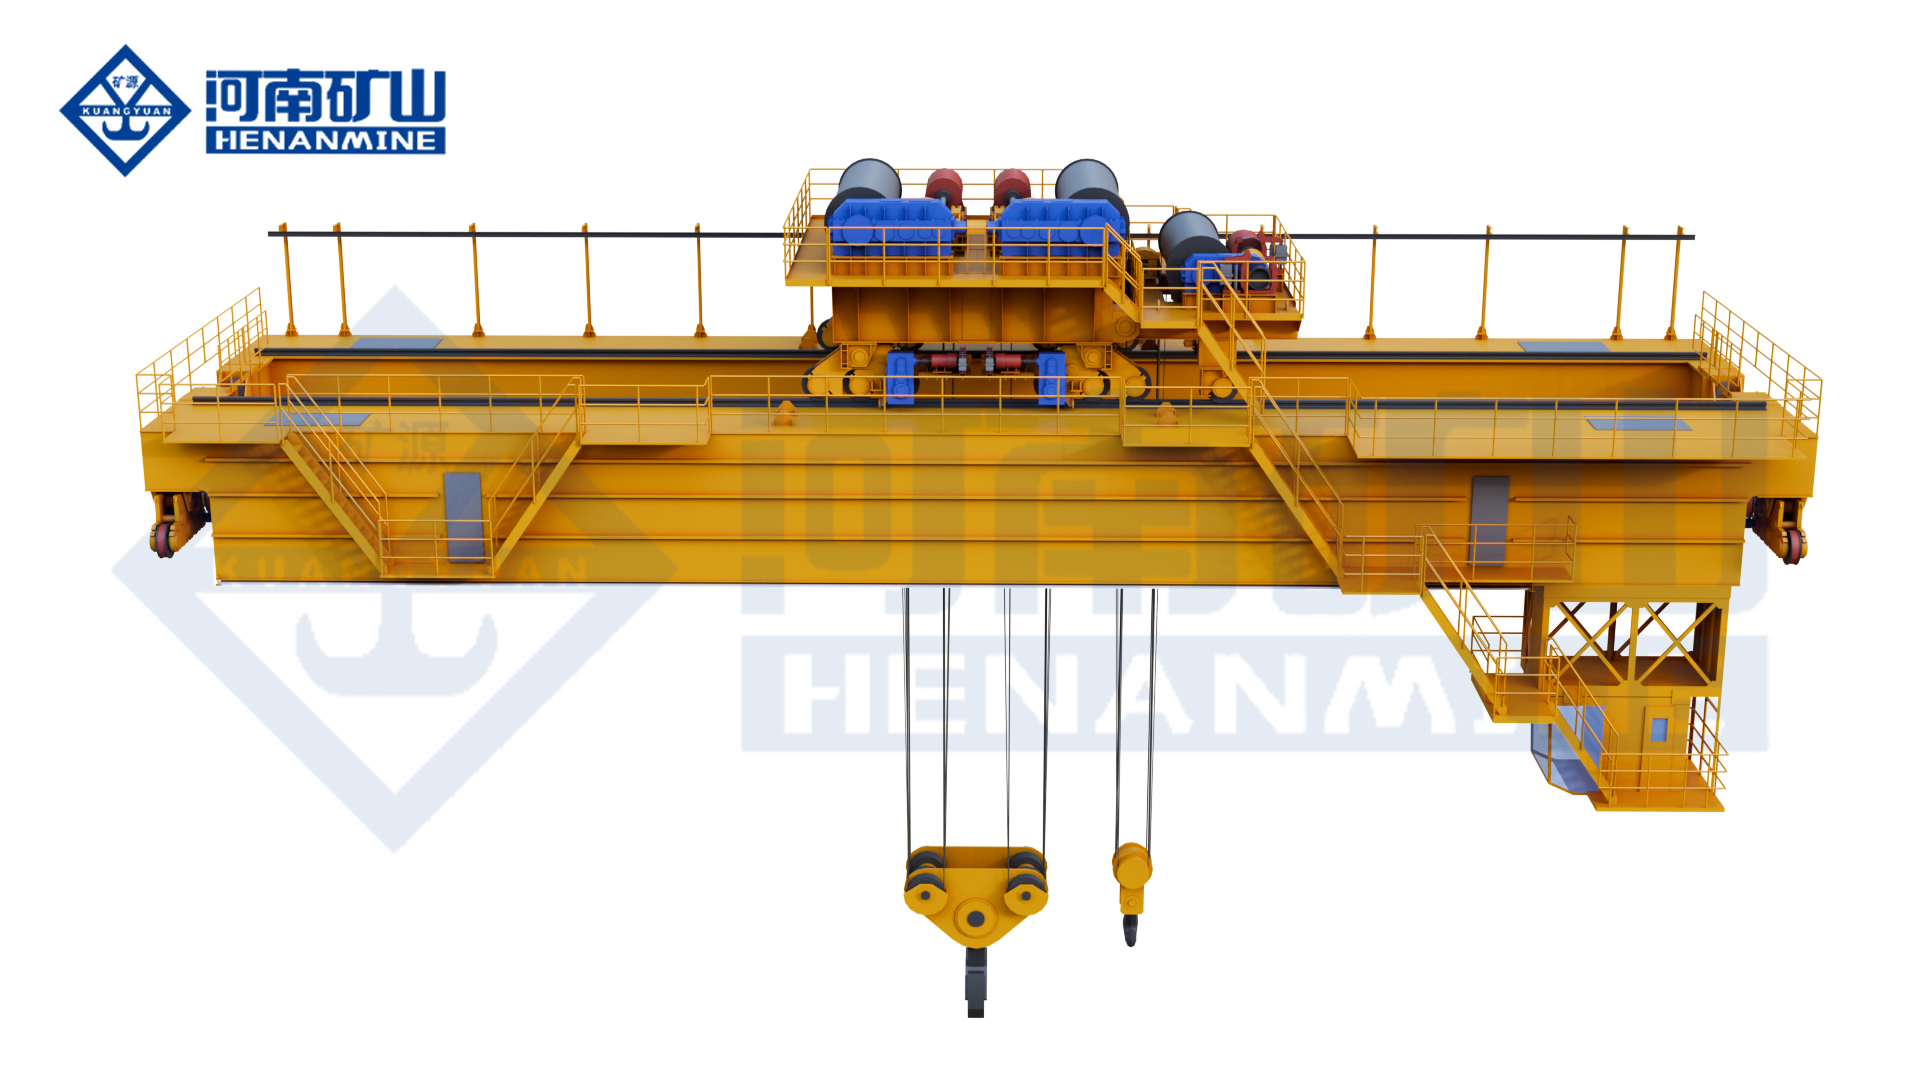
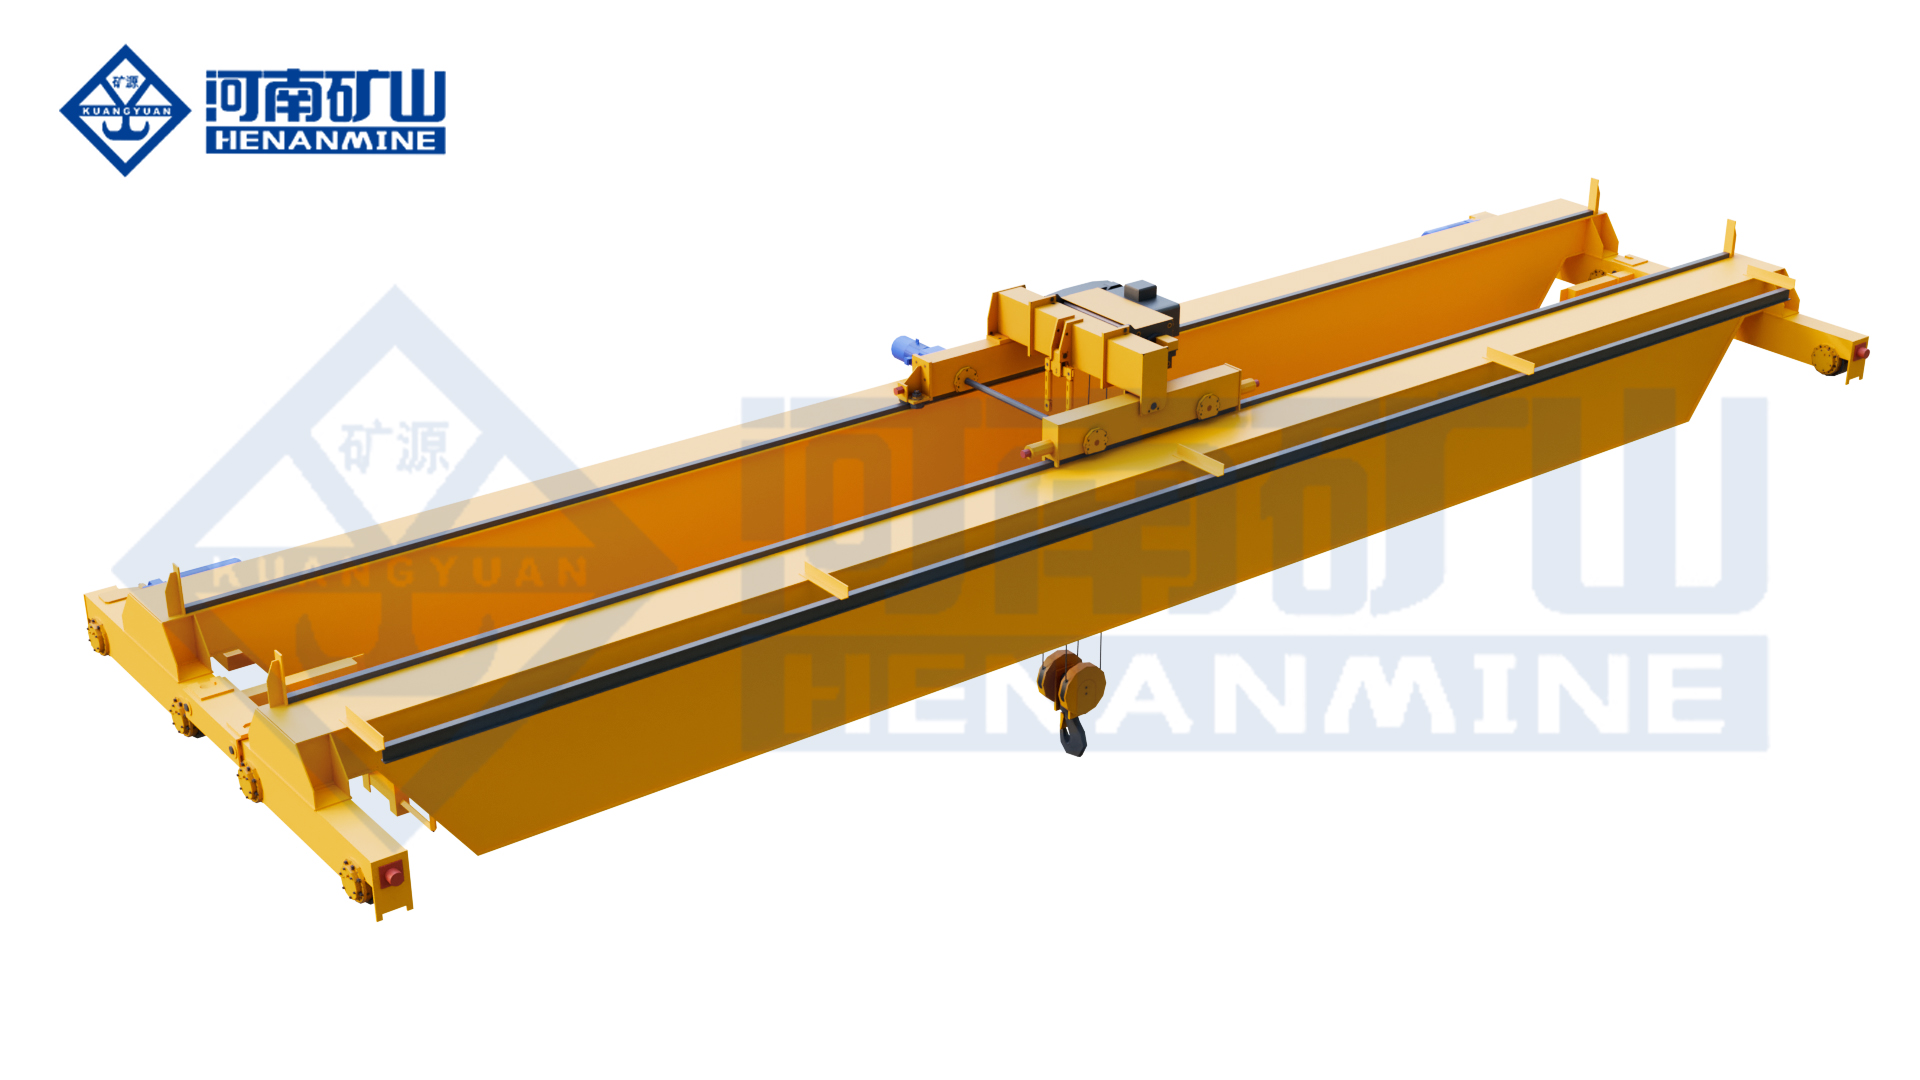
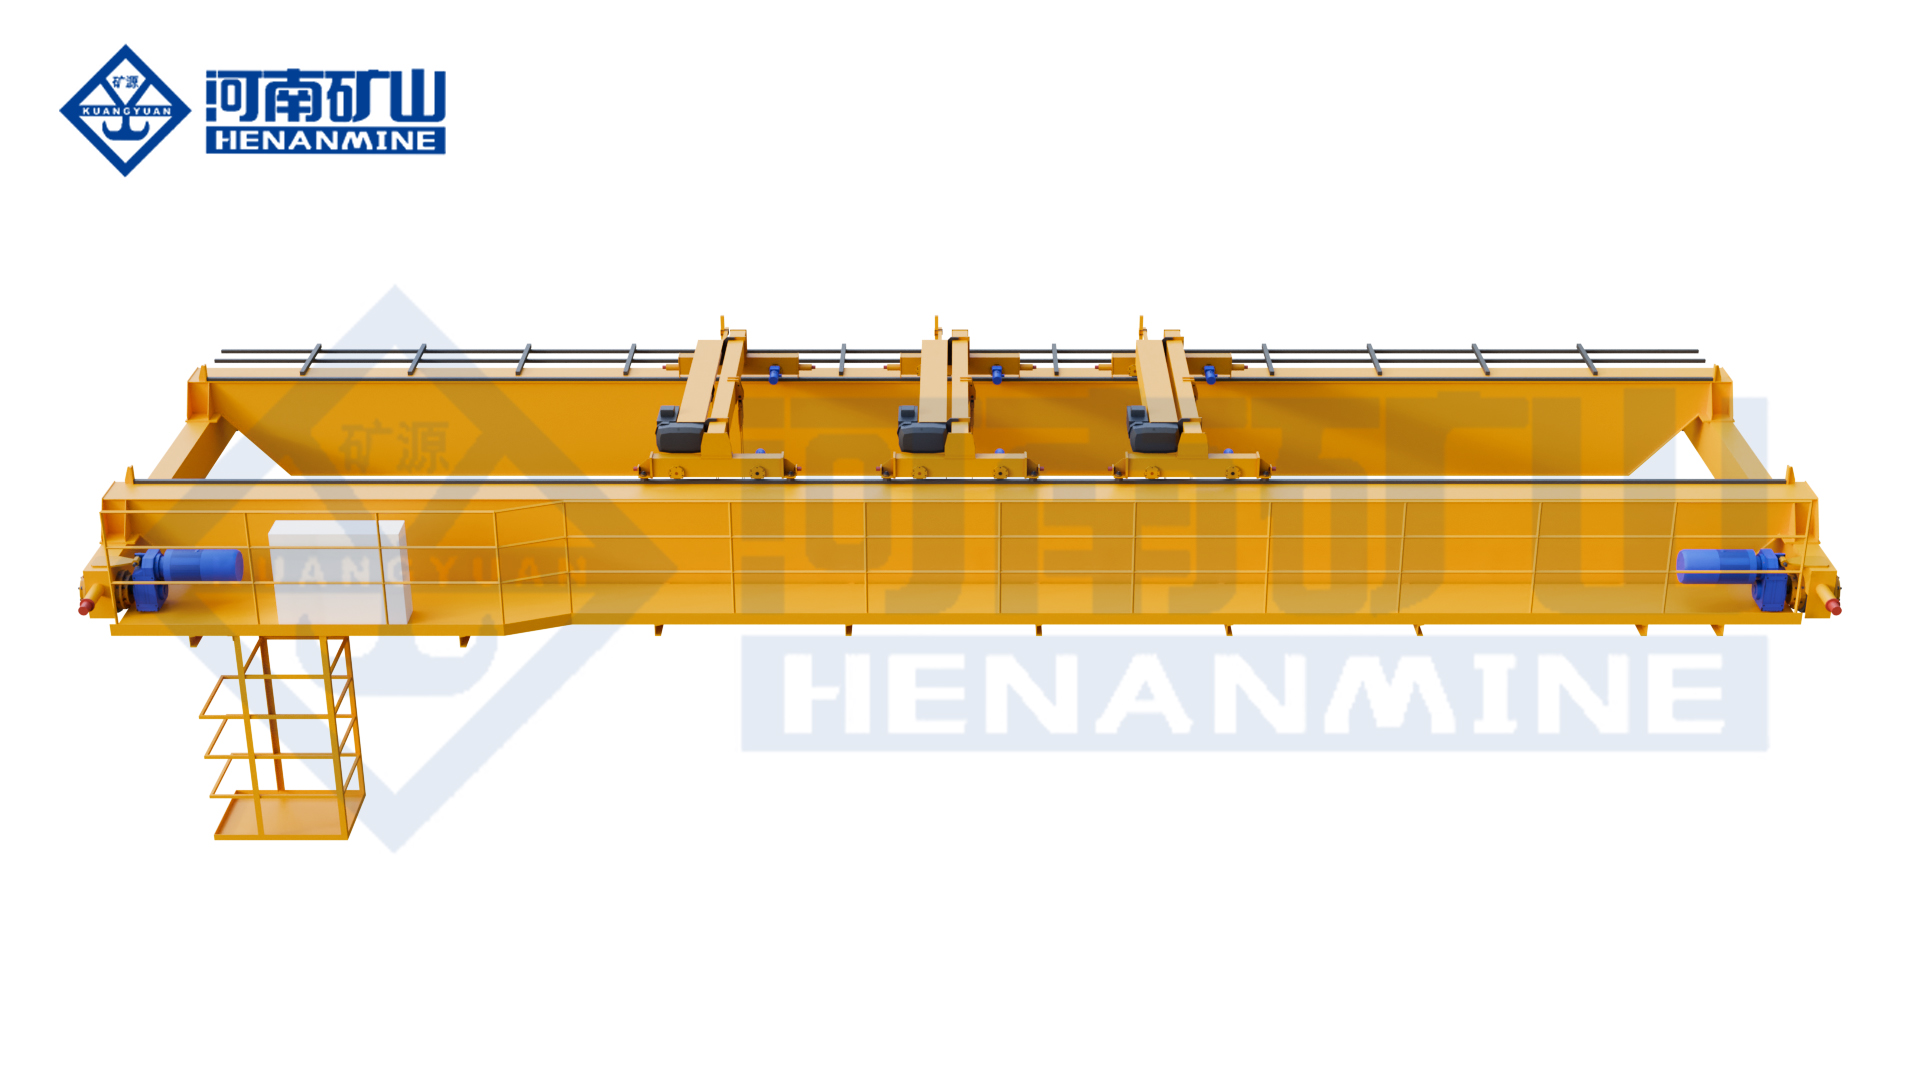
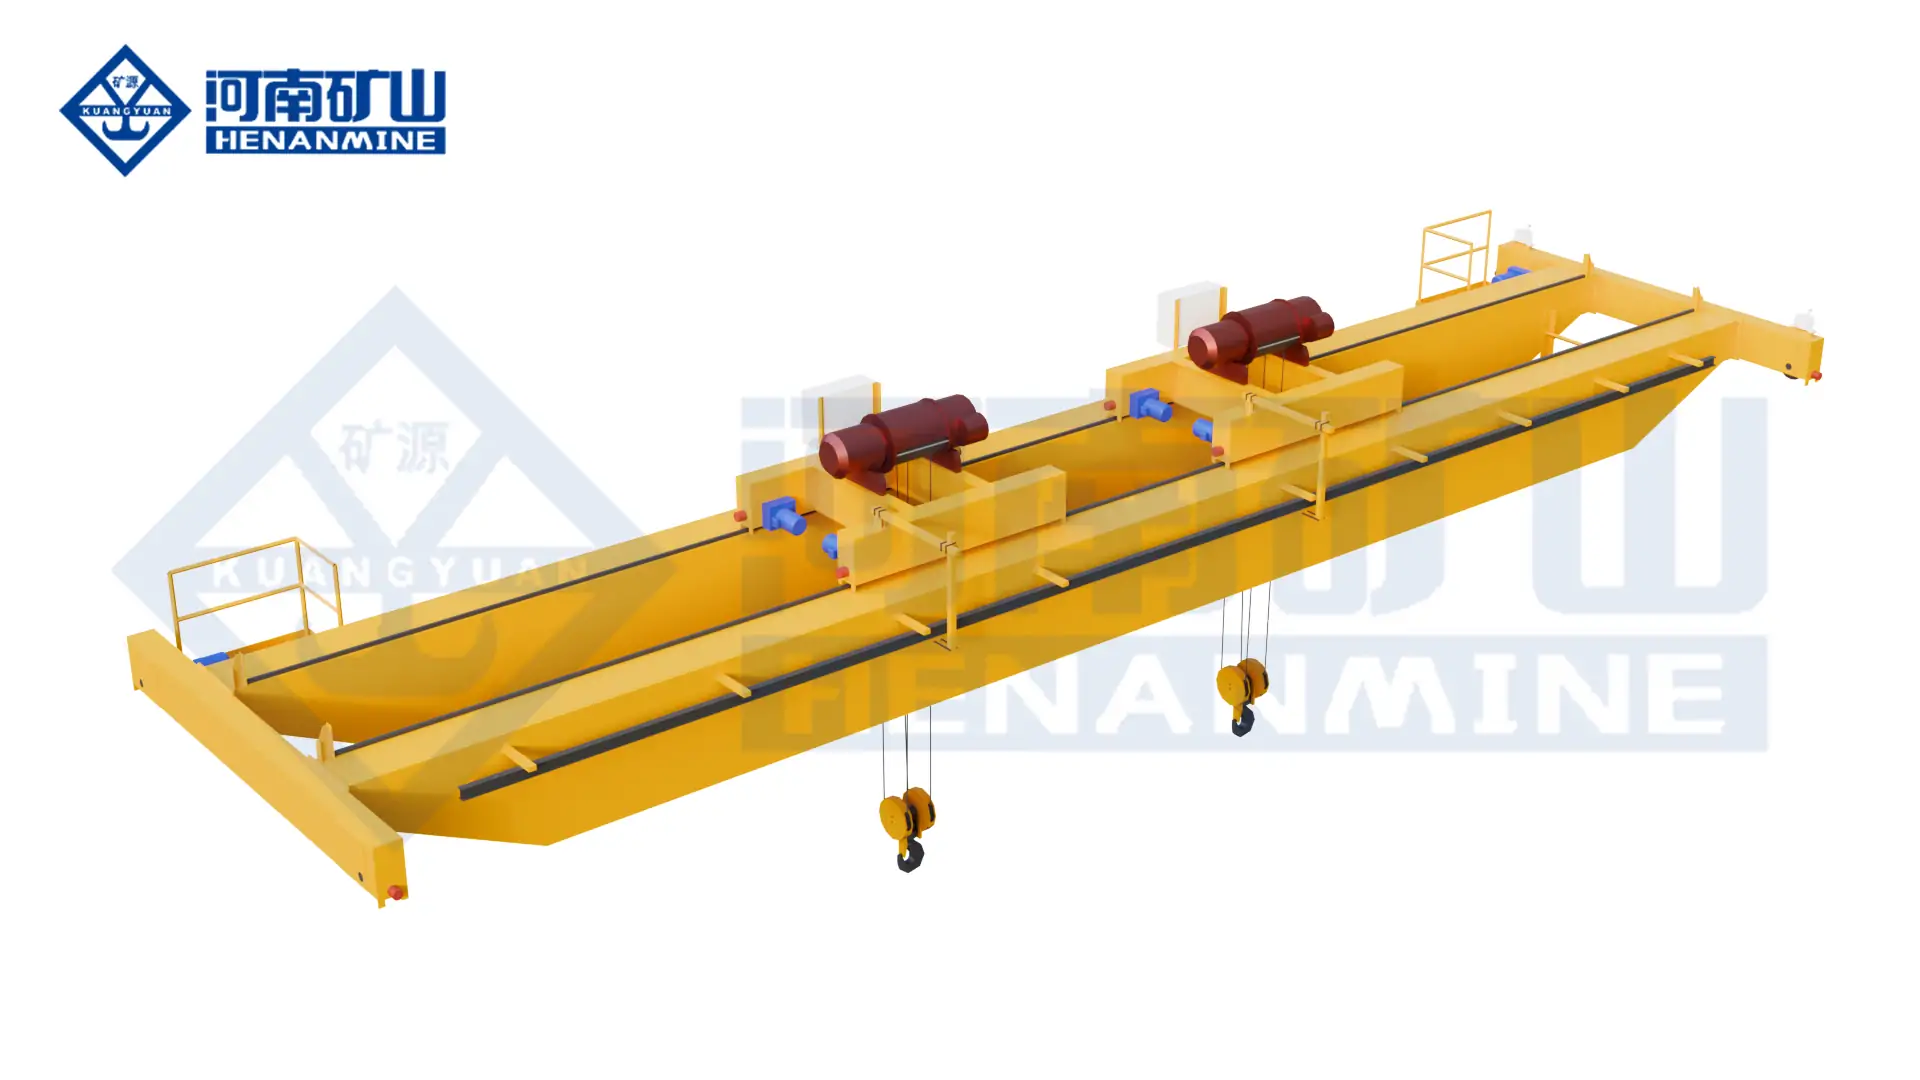
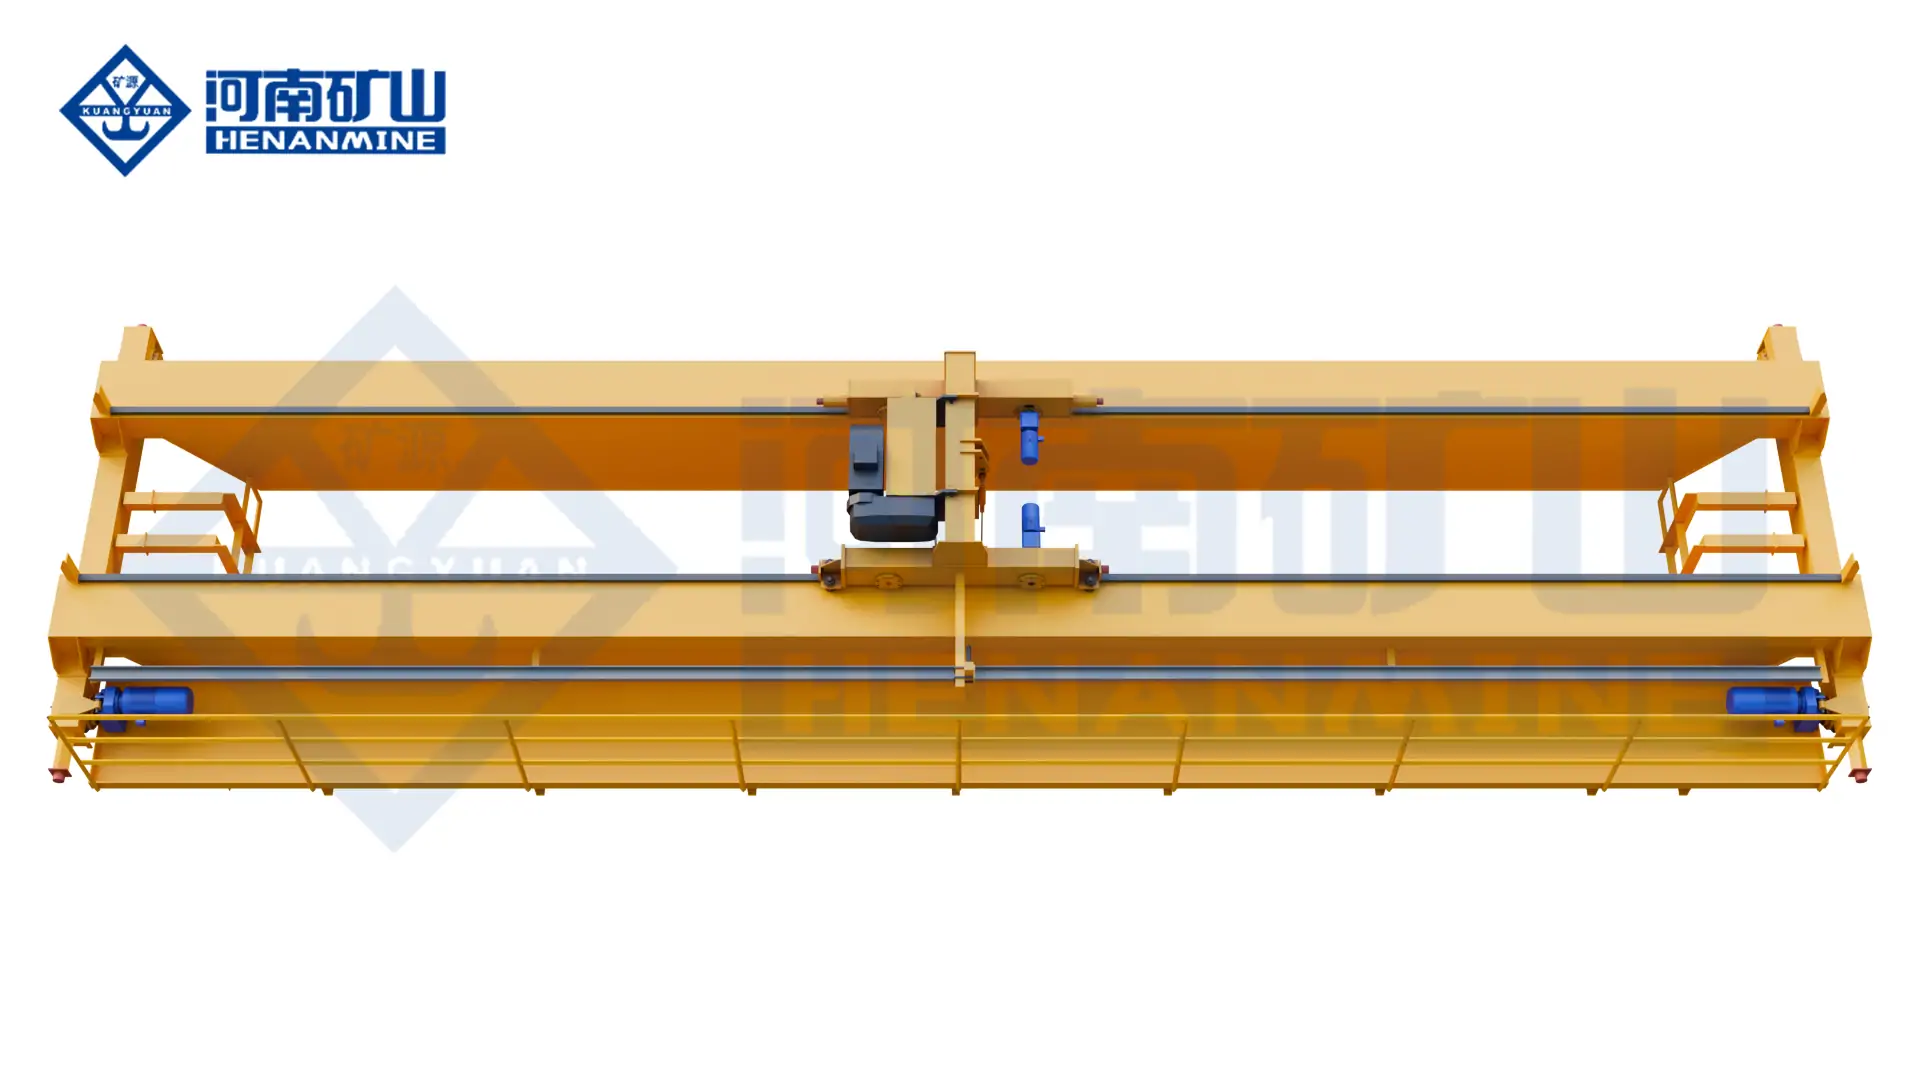
| Double-Girder Overhead Crane | Heavy dies, molds, presses, fixtures and maintenance loads | Higher capacity, stiffness and available hook height for process-duty handling | Duty class, load share, wheel loads, headroom, attachment mass and final approach |
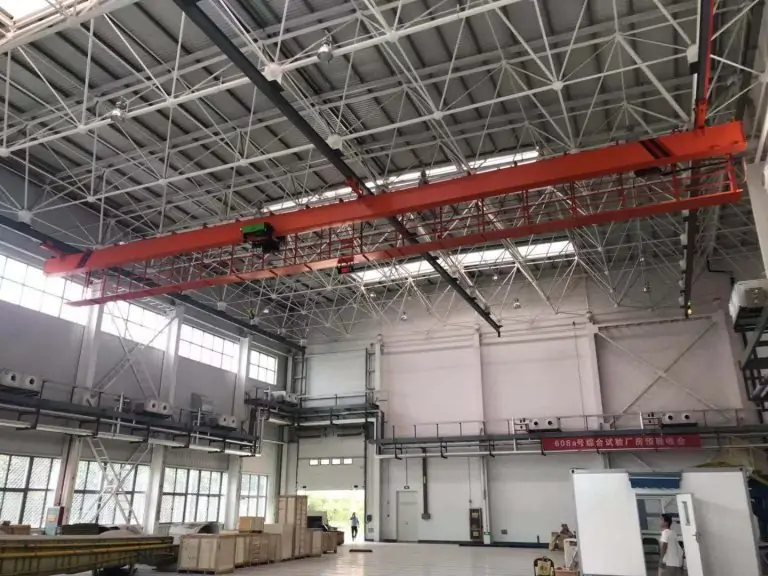
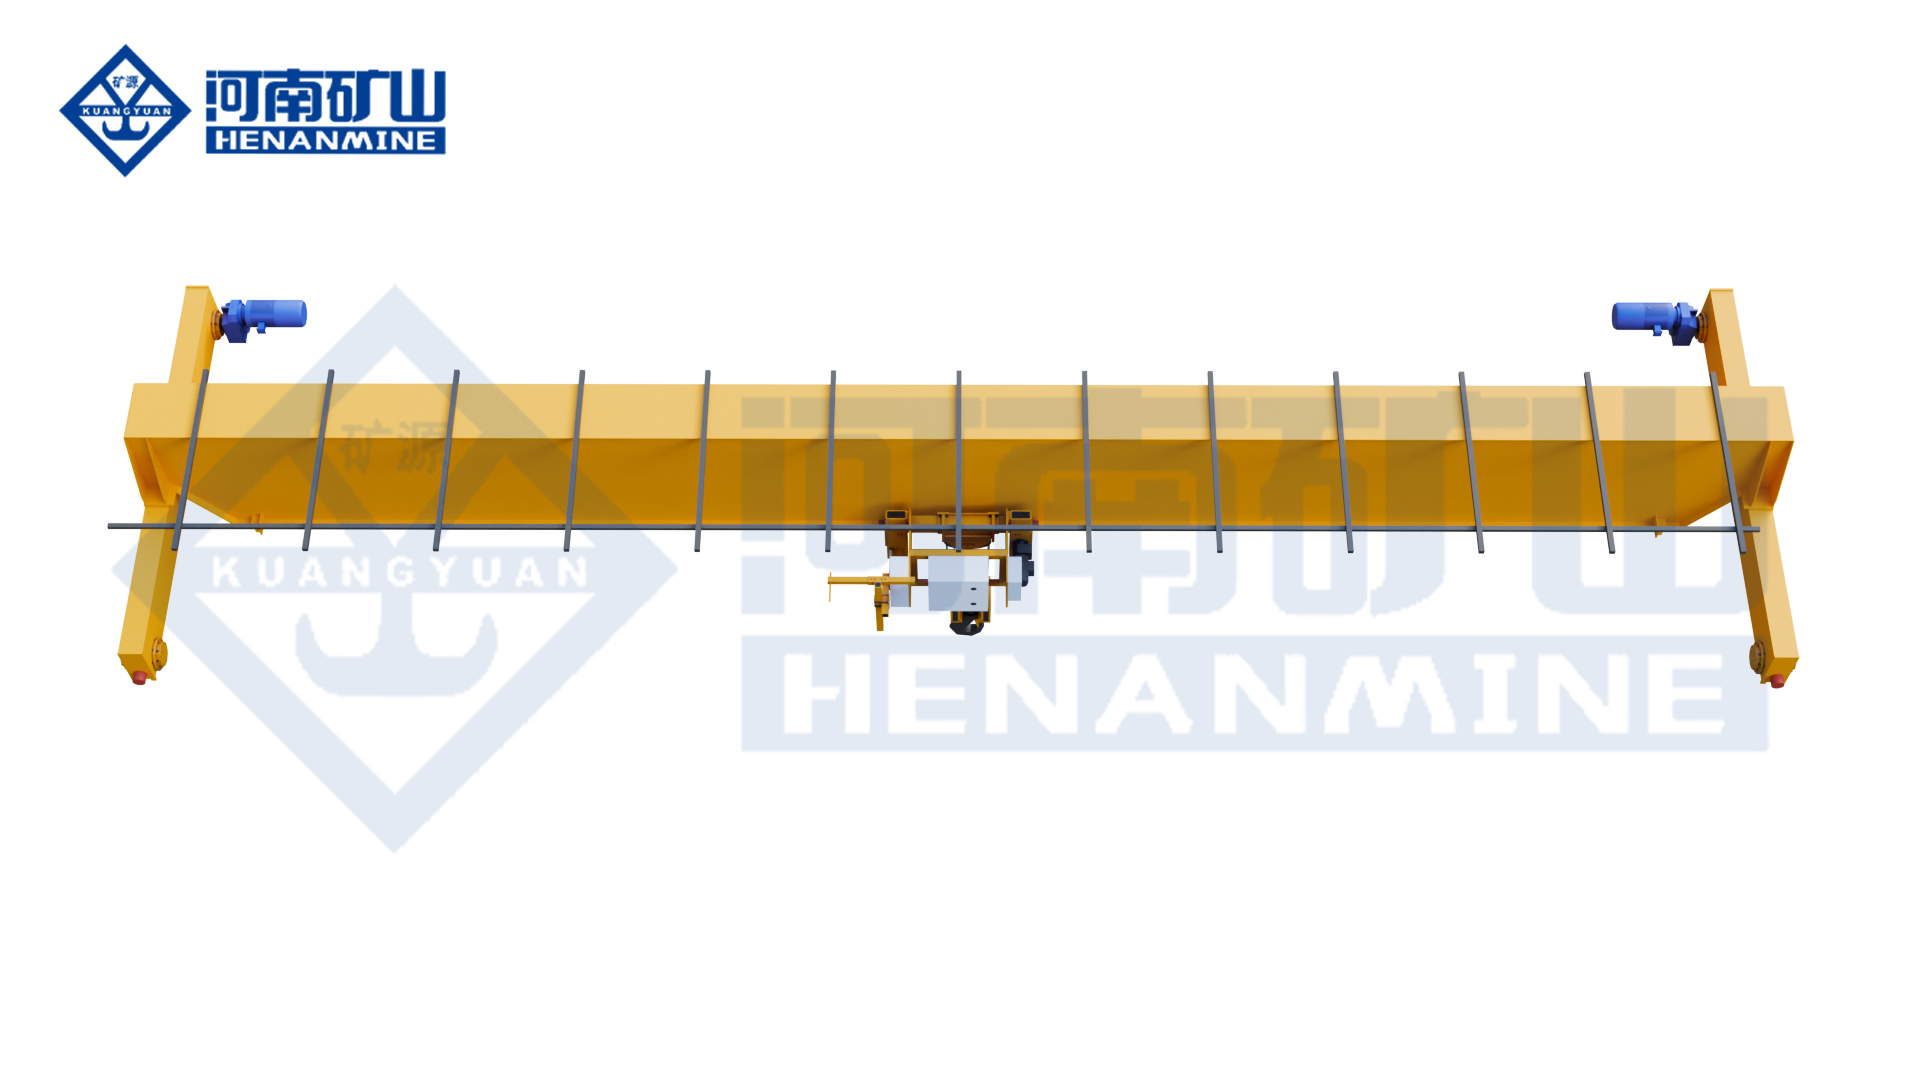
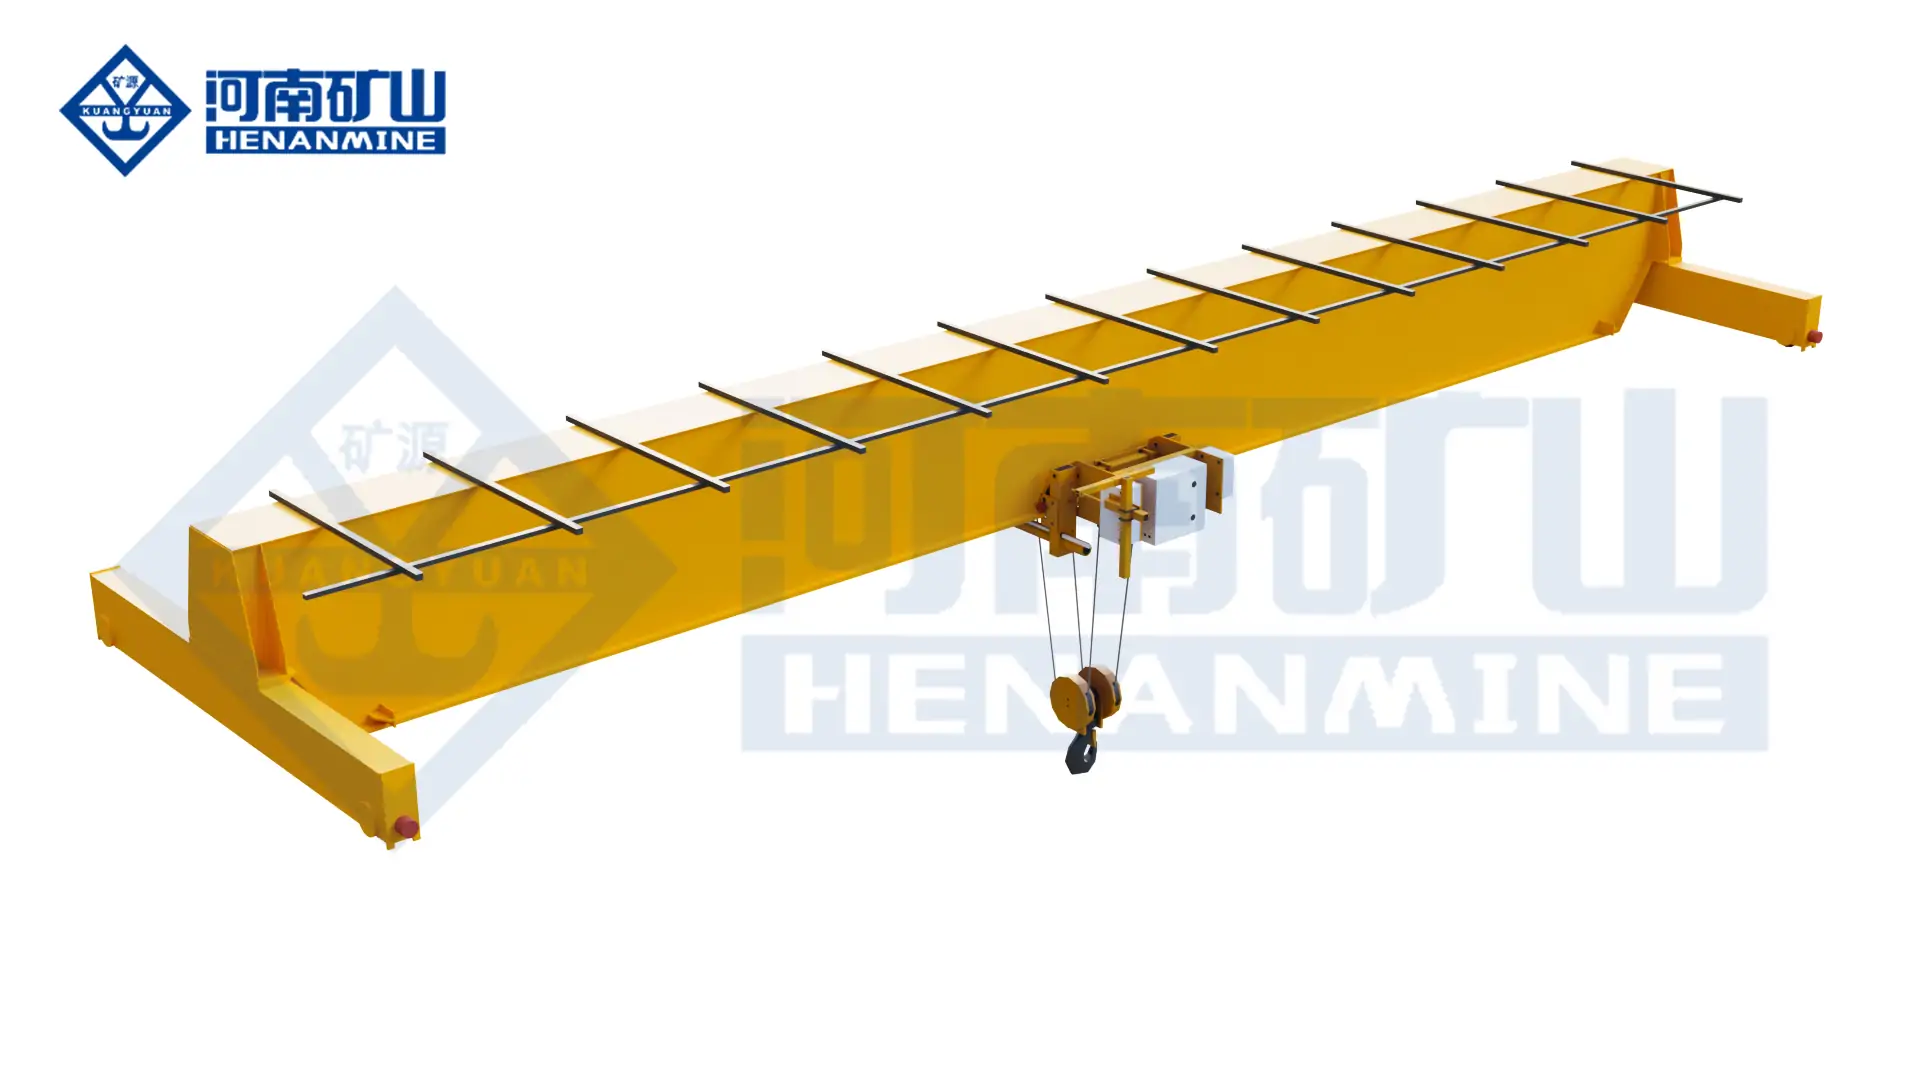
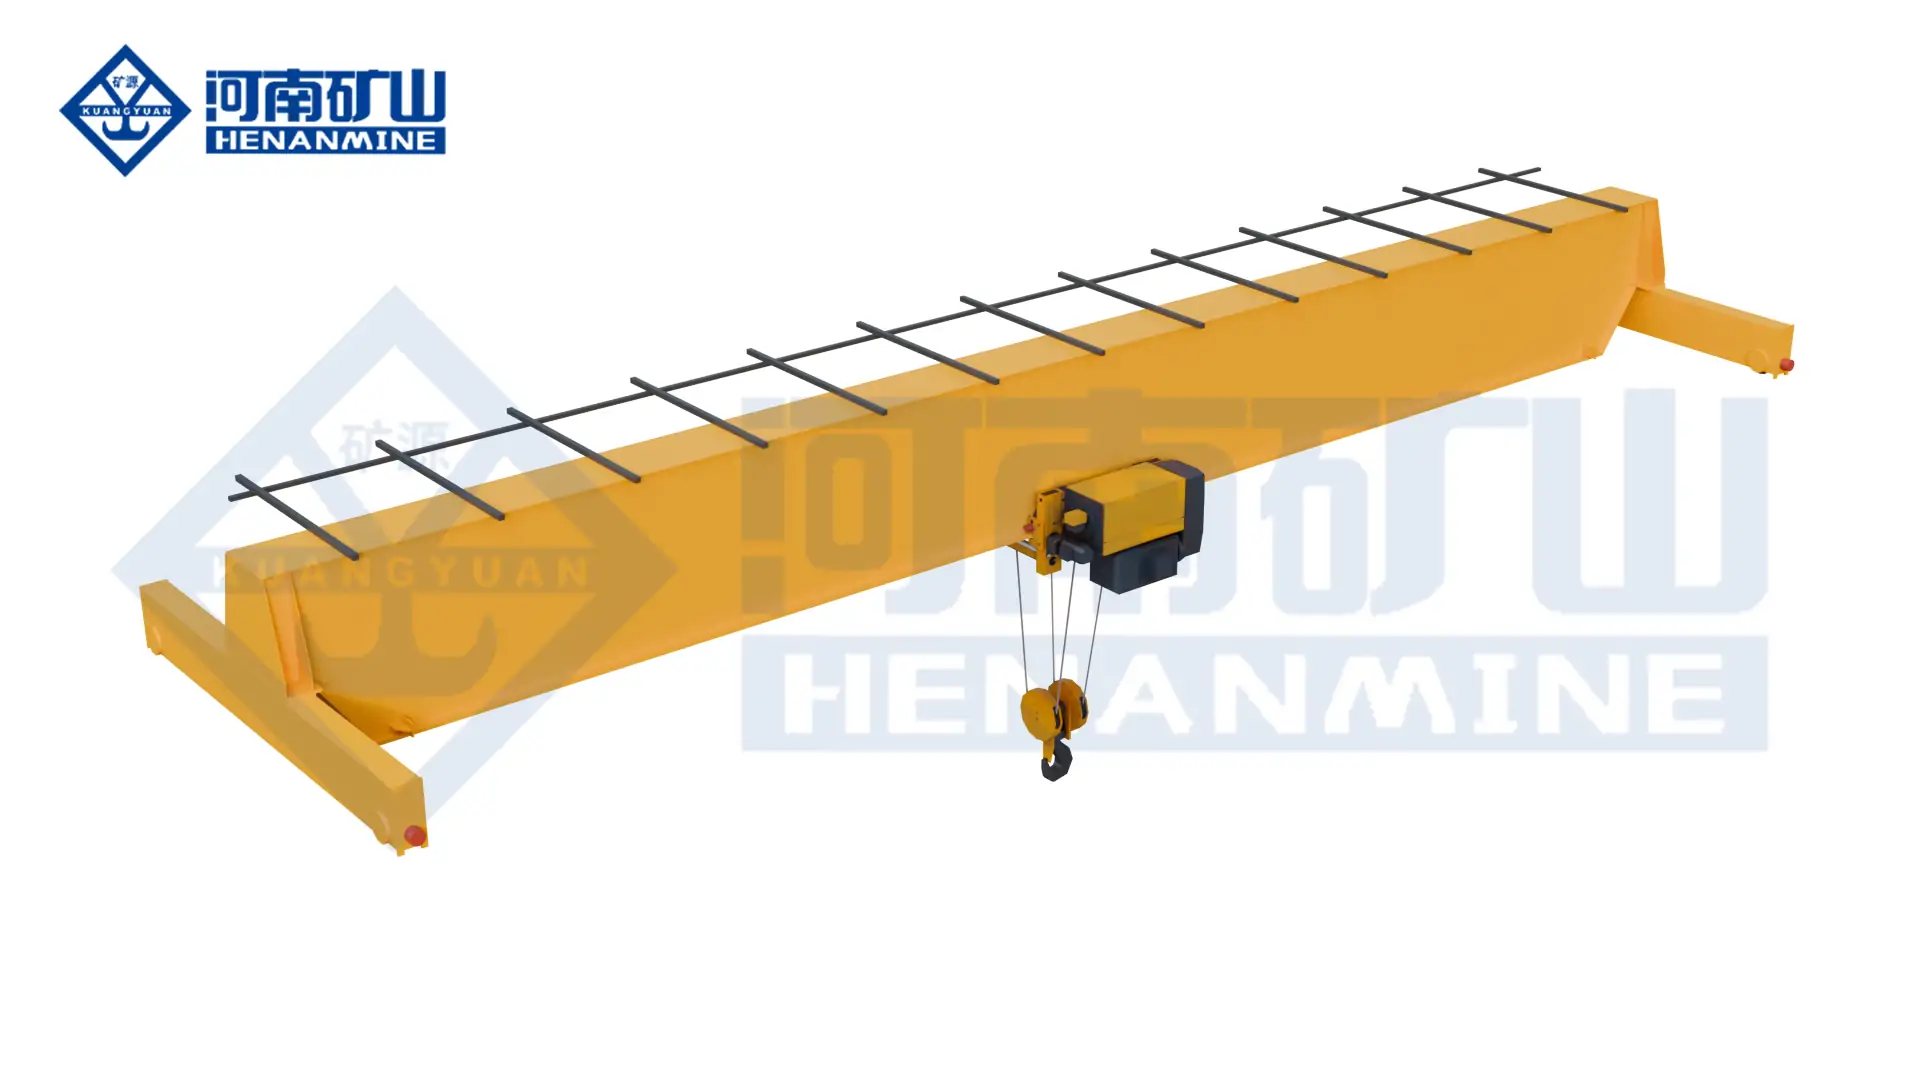
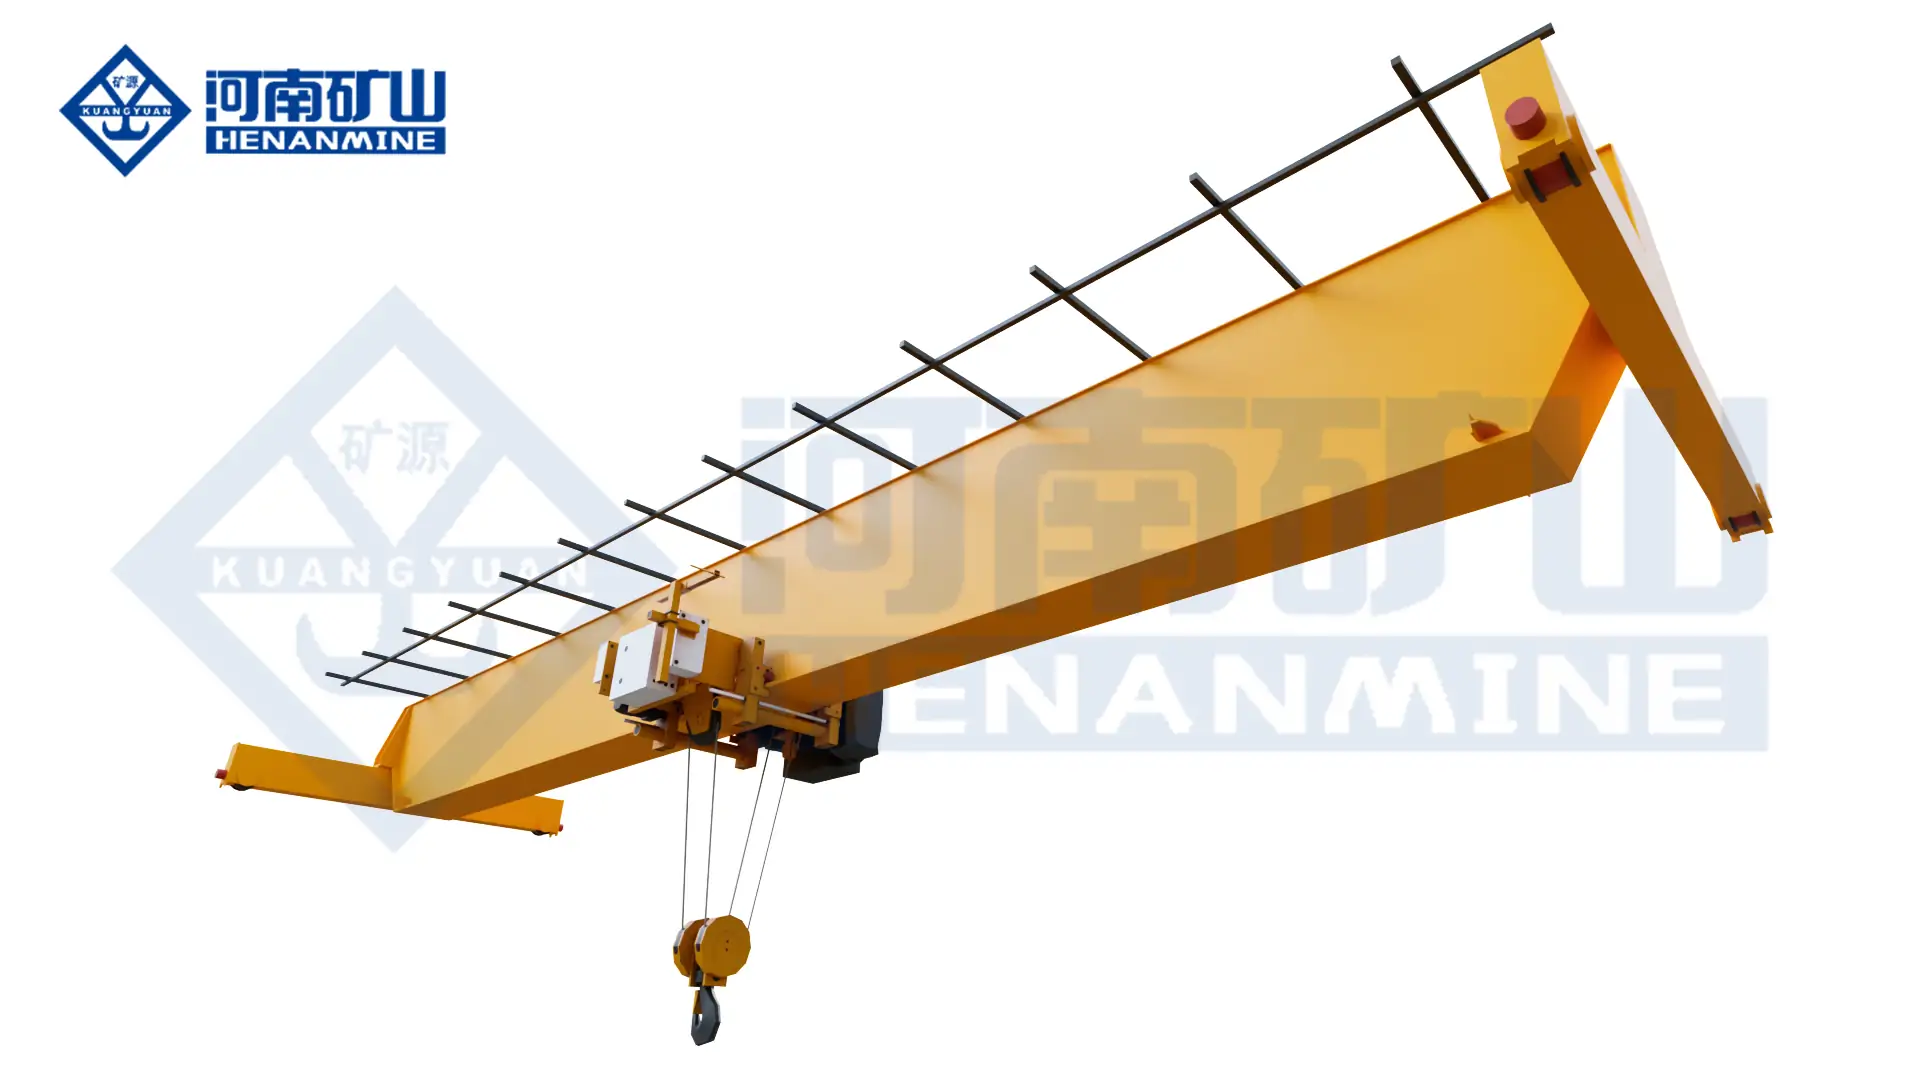
| Single-Girder Low-Headroom Crane | Components, tooling, line maintenance and warehouse service | Compact general-purpose coverage with lower structural mass | Hoist approach, building reactions, actual duty and attachment clearance |
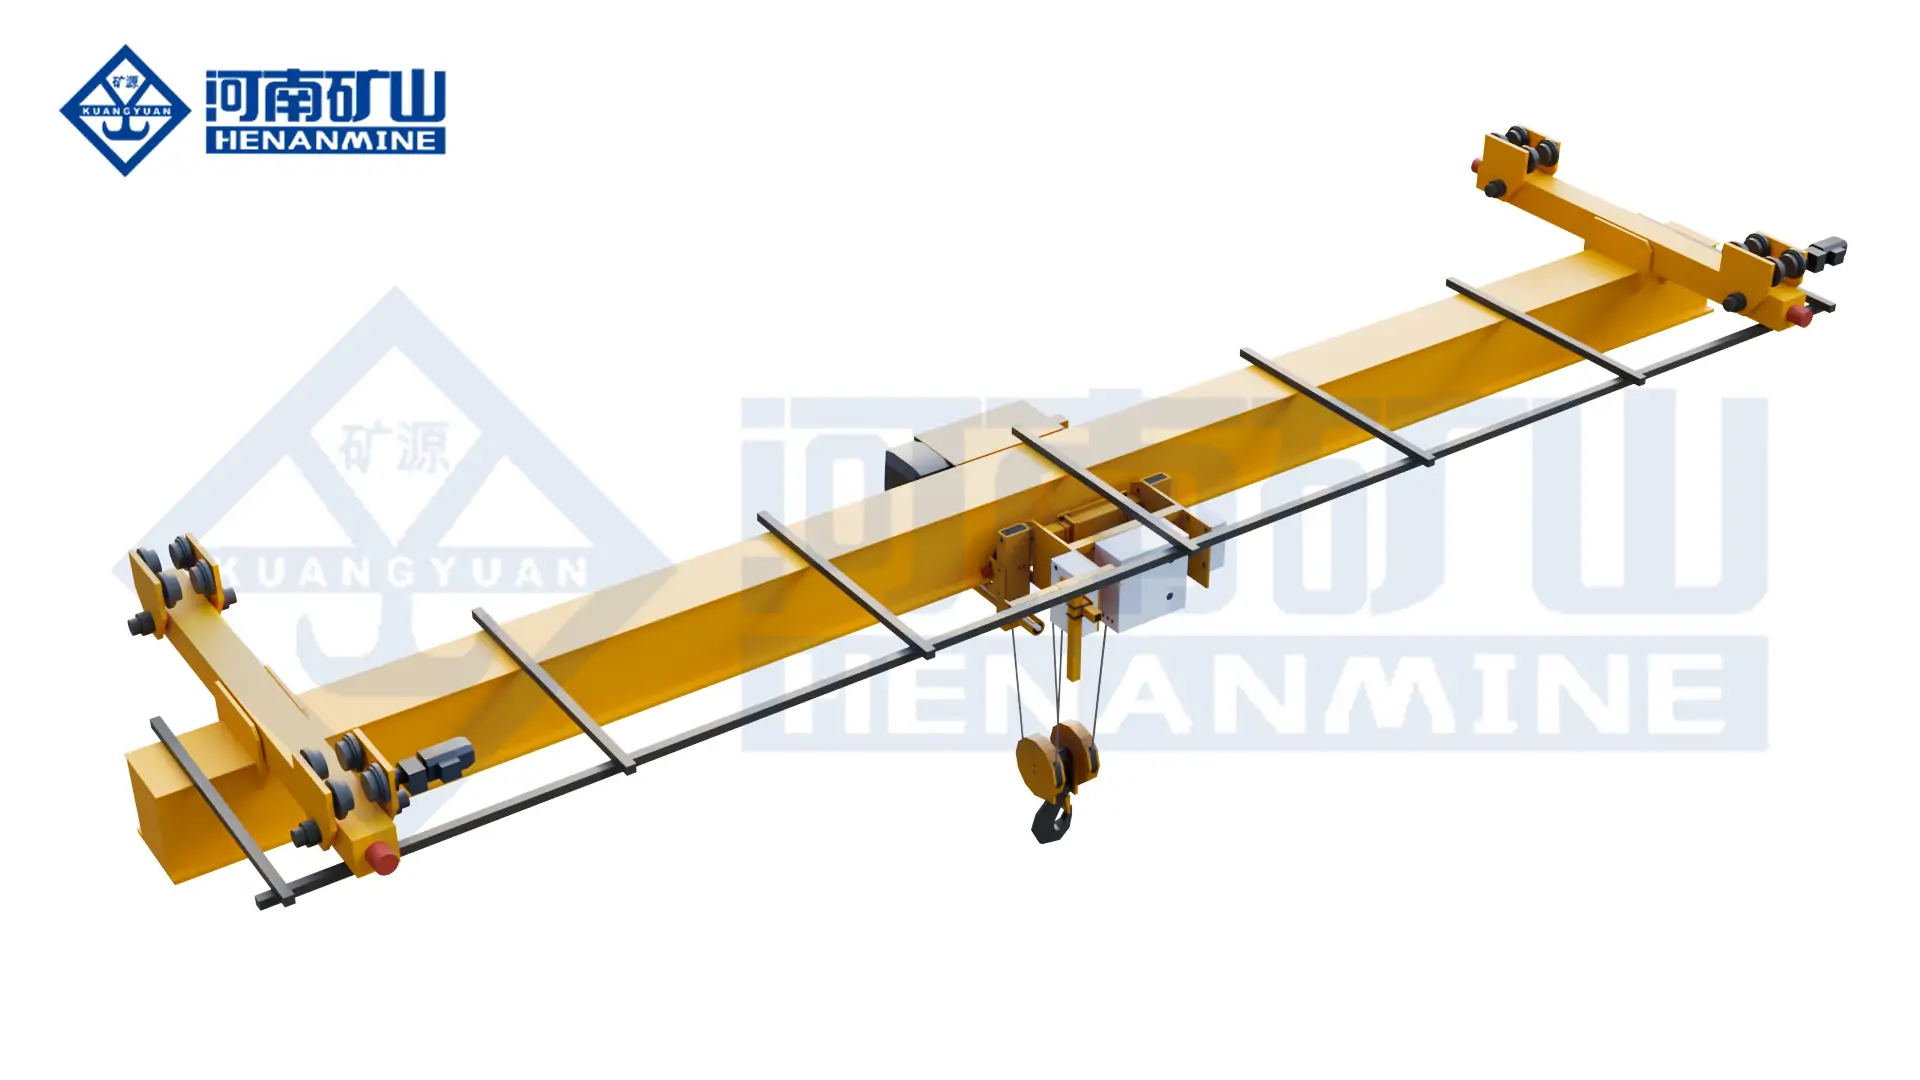
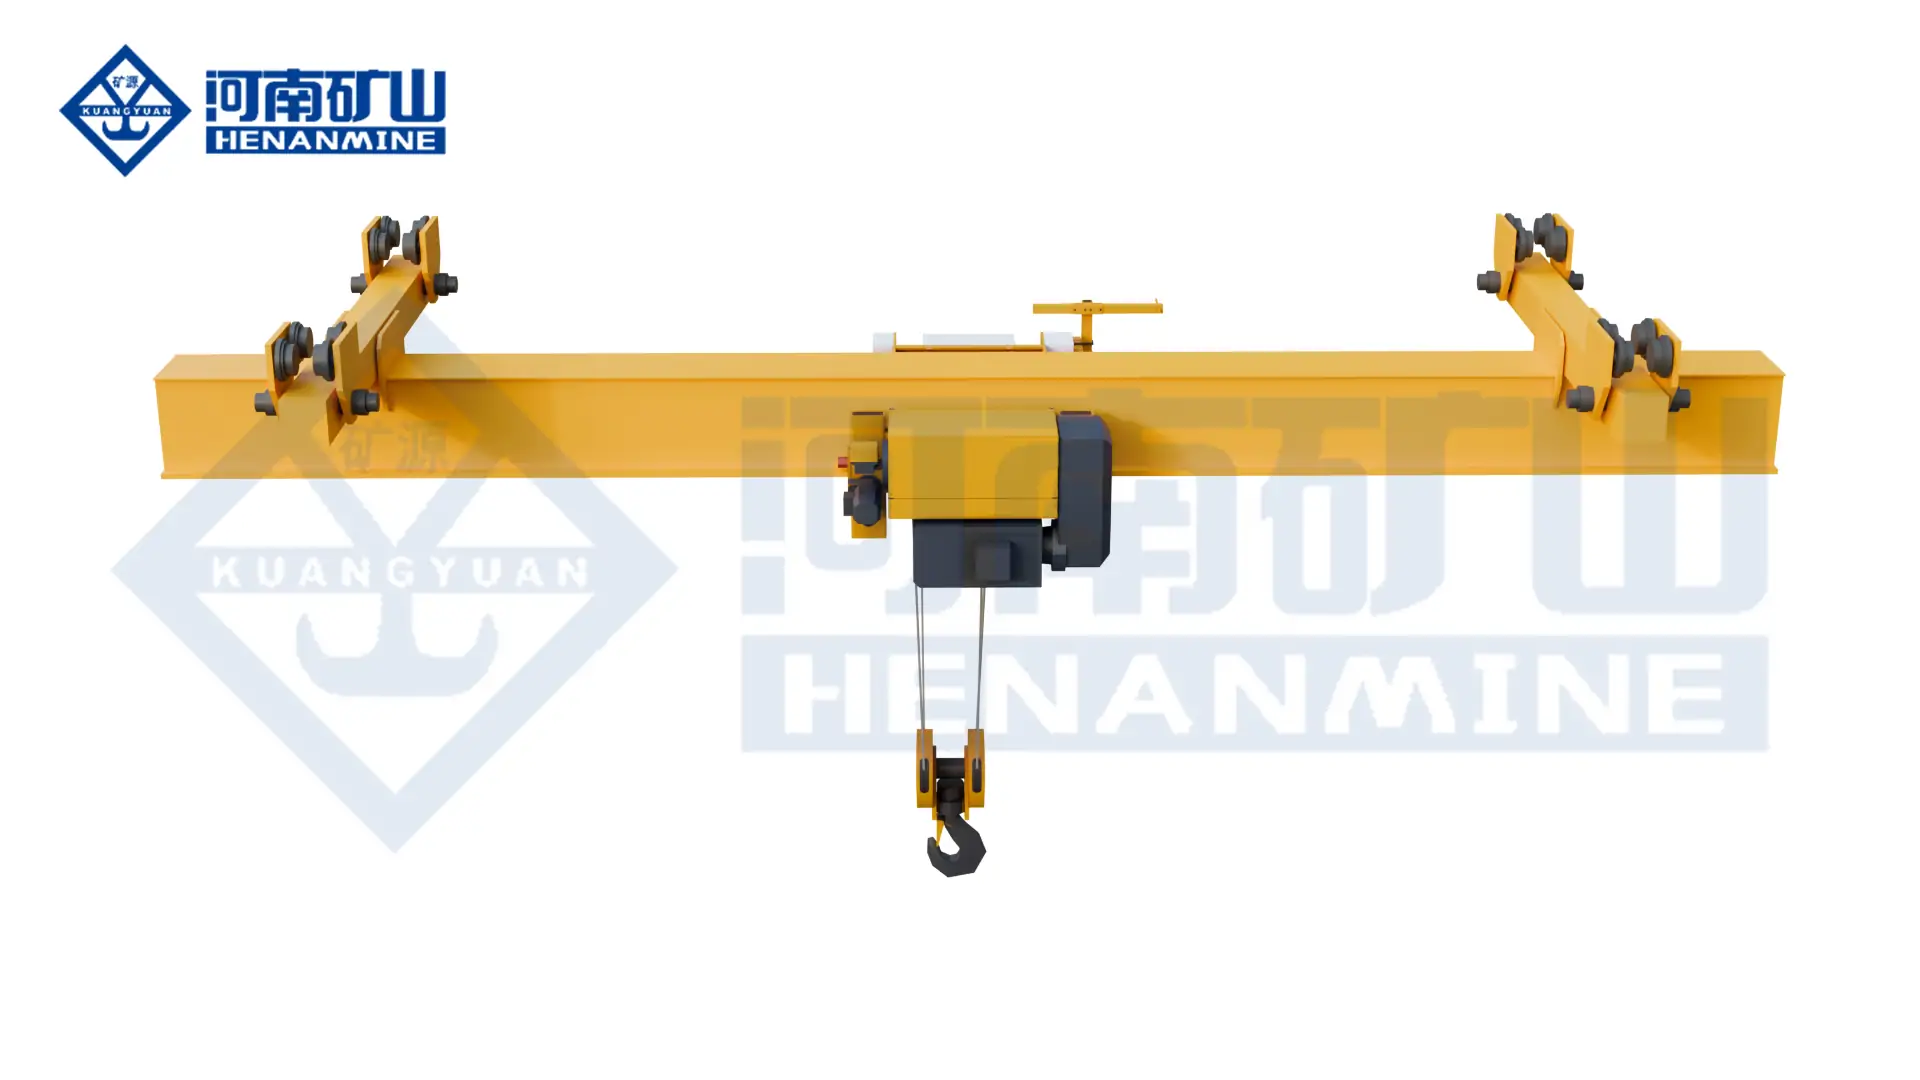
| Underhung or Workstation Crane | Body fixtures, powertrain components and point-of-use assembly | Flexible local coverage above crowded production floors | Roof support, joint and suspension loads, ergonomic force, runway layout and end stops |
| Semi-Gantry Crane | Loading edge, workshop extension and localized machine service | Coverage where only one side of the building can support an elevated runway | Ground rail, building-side reactions, skewing, traffic separation and floor obstruction |
Automotive Press Shop and Die-Handling Crane
Press-shop availability depends on retrieving the correct die set, engaging it safely, traveling along an authorized route and placing it at the defined interface within the production change window.
Die Store Retrieval
The task identifies the die, rack position, mass, center of gravity, approved engagement points and destination. Rack clearances and pickup tolerance are incorporated into the attachment and positioning design.
Grip and Load Confirmation
Mechanical position, locking state, contact or pin engagement and load distribution can be monitored before hoisting. A confirmed signal does not override inspection of damaged or obstructed lifting points.
Protected Transfer
Position tracking, height limits, anti-sway, collision supervision and protected travel corridors control the movement between storage, inspection, maintenance and press-line stations.
Press Ready Handshake
The press, bolster, die cart, clamps, guards and access state must establish an approved transfer condition. The responsibility for each permissive is recorded in the interface matrix.
Precision Placement
Creep speed, load-height feedback, anti-sway and attachment adjustment support final alignment without using press equipment, racks or guides as uncontrolled mechanical stops.
Release and Traceability
Release is enabled only after support, position and station state are confirmed. Task completion records die identity, source, destination, time, alarms and any manual intervention.
Automotive Crane Attachments and Load Interfaces
Die Gripper or Custom Spreader
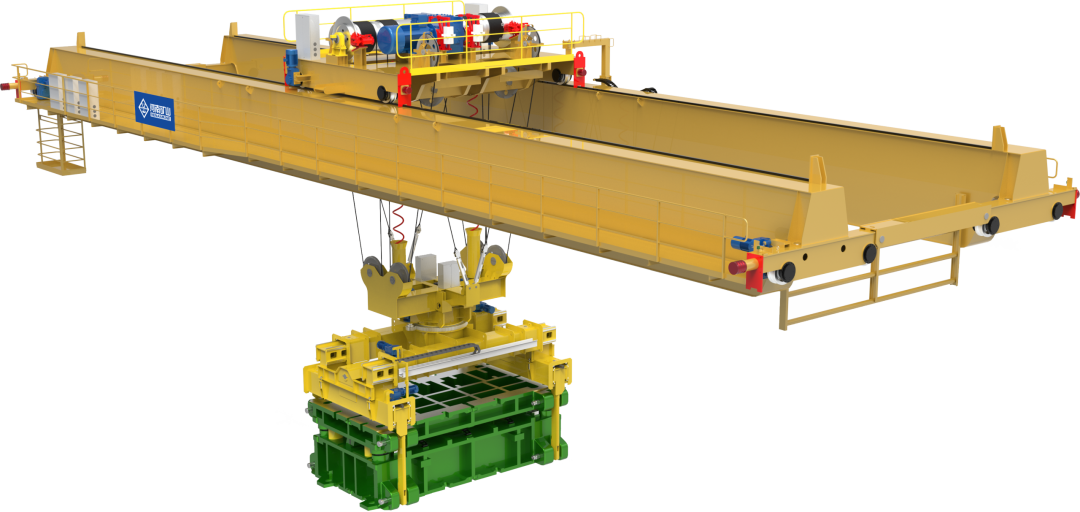
A powered gripper or adjustable spreader supports frequent die retrieval where interfaces can be standardized. Selection covers the complete die range, engagement geometry, adjustment axes, locking confirmation, allowable side load, collision envelope and parking stand.
Attachment deadweight reduces available net load. The crane, attachment and die are therefore evaluated as one suspended system.
Beam, Sling, Tong, Vacuum Device or Manipulator
Four-point beams and certified slings serve defined die lifting points. C-hooks or tongs can serve coils and sheet packs. Vacuum devices can handle suitable panels or sheets, while manipulators support ergonomic component positioning.
Each device requires a declared load range, proof test, inspection criteria and energy-loss response. Surface condition, porosity, oil, curvature and temperature are included where vacuum or magnetic principles are considered.
Die Turning
Turning or inversion requires an engineered turning device, two-hook arrangement or dedicated station with defined load share and control sequence. Side pulling, dragging and improvised turnover are excluded.
Component Protection
Replaceable non-marking contact pads, controlled clamping force, soft motion profiles and approved support geometry protect machined surfaces, painted parts and precision fixtures.
Attachment Changeover
A multi-purpose crane requires a safe connection method, identified services, parking stands, retained capacity, changeover time and recovery procedure for an incomplete connection.
Capacity, Duty Class and Positioning Performance
Gross Load and Net Capacity
Crane rated capacity must cover the heaviest die, mold, fixture or component plus the complete below-the-hook attachment and any suspended auxiliaries. The crane manufacturer accounts for the hook block and reeving within the machinery design. Eccentric centers of gravity and uneven load share are checked separately.
Duty from the Production Profile
ISO, FEM or CMAA classification is derived from operating hours, starts, load spectrum, travel, reversing and production consequences. A crane lifting the maximum die only occasionally can have a different duty from a lighter crane cycling continuously on an assembly line.
Accuracy and Repeatability
Positioning claims define measurement point, load, speed, axis, repeatability, environmental conditions and acceptance method. Structural deflection, rope stretch, sway, attachment compliance and rack or press tolerance all influence final placement.
Performance Data Required
- Maximum and minimum load with attachment
- Load dimensions, lifting points and center-of-gravity range
- Lifts per hour, shifts, annual hours and load spectrum
- Source, destination, travel distance and lift height
- Changeover time and required availability
- Final approach speed and placement tolerance
- Abnormal recovery and retained-load strategy
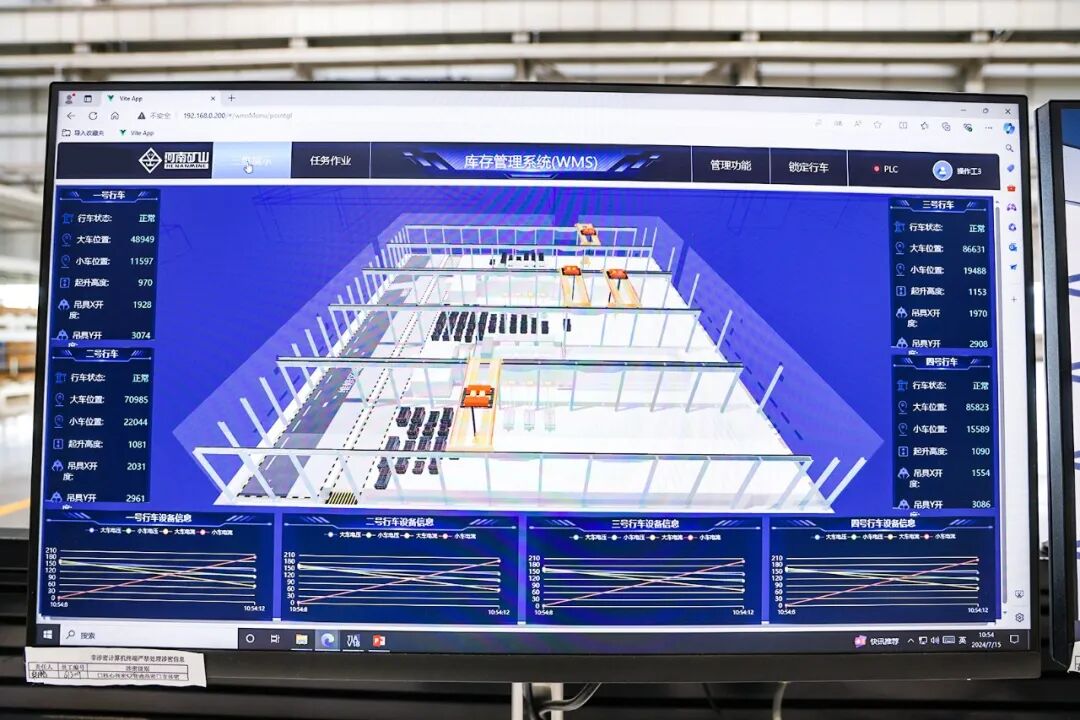
Automation, WCS and Production-Line Integration
Task and Load Identity
WCS, MES, barcode, RFID or operator confirmation associates the physical die or component with mass, coordinates, process status and destination. Unidentified or conflicting loads enter a controlled exception state.
Position and Anti-Sway
Absolute or referenced coordinates, controlled acceleration, sway reduction, load-height feedback and final approach logic support stable movement without contact-based correction.
Press and Station Handshake
Ready, occupied, guarded, clamped, transfer enabled, release authorized, complete and fault states are exchanged with presses, die carts, racks, gates and maintenance systems.
Protected Areas and Collision Control
Restricted volumes, temporary maintenance zones, crane-to-crane separation, obstacle detection and speed-limited approaches are implemented under the approved risk assessment.
Operating Modes
Automatic, remote, local maintenance and recovery modes have defined authority, speed limits, permissives and transition conditions. Active mode and control ownership remain unambiguous.
Diagnostics and Recovery
Event logs, cycles, loads, sensor states and alarms support maintenance. Recovery covers incomplete gripping, lost position, unavailable destination, failed communications and power interruption.
Safety Functions and Environmental Boundaries
Suspended-Load Exclusion
Pedestrian workstations, vehicle lanes and operator positions are kept outside the suspended-load path. Automatic operation uses controlled access and a defined safe state for zone entry.
Attachment Permissive
Hoisting and travel permissions can depend on verified engagement, load range and attachment configuration. Release remains inhibited until the load is supported and the destination is authorized.
Press and Robot Interlocks
Press motion, robot zones, die-cart travel, clamps, guards and crane movement are coordinated so that conflicting commands cannot create an uncontrolled exposure.
Overload, Limits and Brakes
Rated-capacity protection, normal and final motion limits, brakes, buffers, travel warnings and monitored speed zones are selected under the governing code and risk assessment.
Paint and Solvent Areas
Explosion-protected equipment is supplied only where the approved hazardous-area classification identifies zones, gas or vapor groups, temperature class and equipment protection requirements.
Battery Production Boundary
Cell manufacturing, module assembly and finished-pack handling can have different dry-room, cleanliness, chemical, dust and fire conditions. The site assessment determines the applicable crane package.
Runway, Building and Maintainability Interfaces
Existing Building Verification
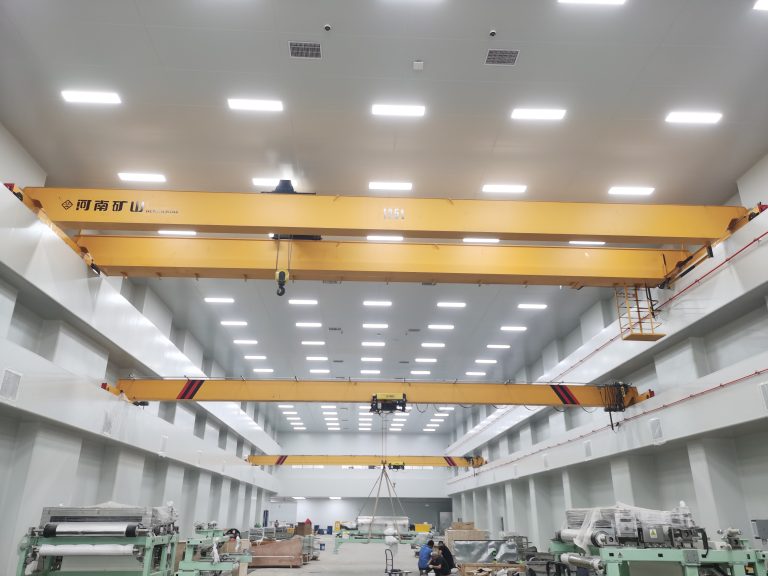
Reuse requires verification of rails, runway beams, roof trusses or suspension points, brackets, columns, connections, foundations, fatigue history and measured condition. Maximum and minimum wheel reactions, lateral forces and buffer loads are issued for structural review.
Clearance and Production Coordination
Bridge, trolley, attachment and load envelopes are checked against presses, die racks, robots, conveyors, ducts, cable trays, lighting and fire systems. Installation is planned around production shutdowns and protected line areas.
Maintenance Strategy
Access platforms, safe parking, isolation, inspection positions, rope and brake service, attachment maintenance and component-removal routes are defined before procurement. Critical spare strategy reflects the production consequence of downtime.
Site Data Required
- Building, runway and production-layout drawings
- Rail or suspension-point survey and allowable reactions
- Press, rack, robot, conveyor and utility envelopes
- Attachment parking and maintenance access
- Power, grounding and communication networks
- Erection opening, laydown area and shutdown window
- Environmental and hazardous-area documents
Applicable Standards and Acceptance Testing
The contract identifies the governing jurisdiction, crane design code, electrical standard and below-the-hook lifting-device rules. Common reference frameworks include ISO 4301 for classification, ISO 9927 for inspections and ISO 12480-1 for safe use; EN 13001 and EN 15011; CMAA 70 or CMAA 74 with applicable ASME B30 requirements; and ASME B30.20 with ASME BTH-1 for relevant lifting devices.
IEC 60204-32 can govern electrical equipment for hoisting machines, while ISO 13849-1 or IEC 62061 can inform safety-related controls. IEC 60529 addresses enclosure ingress ratings and ISO 12944 can inform coating selection. ATEX, IECEx, NEC or other hazardous-location requirements apply only where the approved project classification establishes that scope. Local law and the signed specification remain controlling.
Design Review
Confirm load cases, classification, general arrangement, runway reactions, attachment, die range, placement performance, safety functions, interfaces and maintenance access.
Factory Acceptance Test
Verify assemblies, drives, brakes, limits, load protection, attachment logic, safety functions, interface simulation, operating modes, diagnostics and contracted documentation.
Site and Production Acceptance
Test proof loads, representative dies, all source and destination stations, cycle time, placement, interlocks, restricted zones, communications loss and manual recovery.
Published Automotive Mould-Handling Crane Project
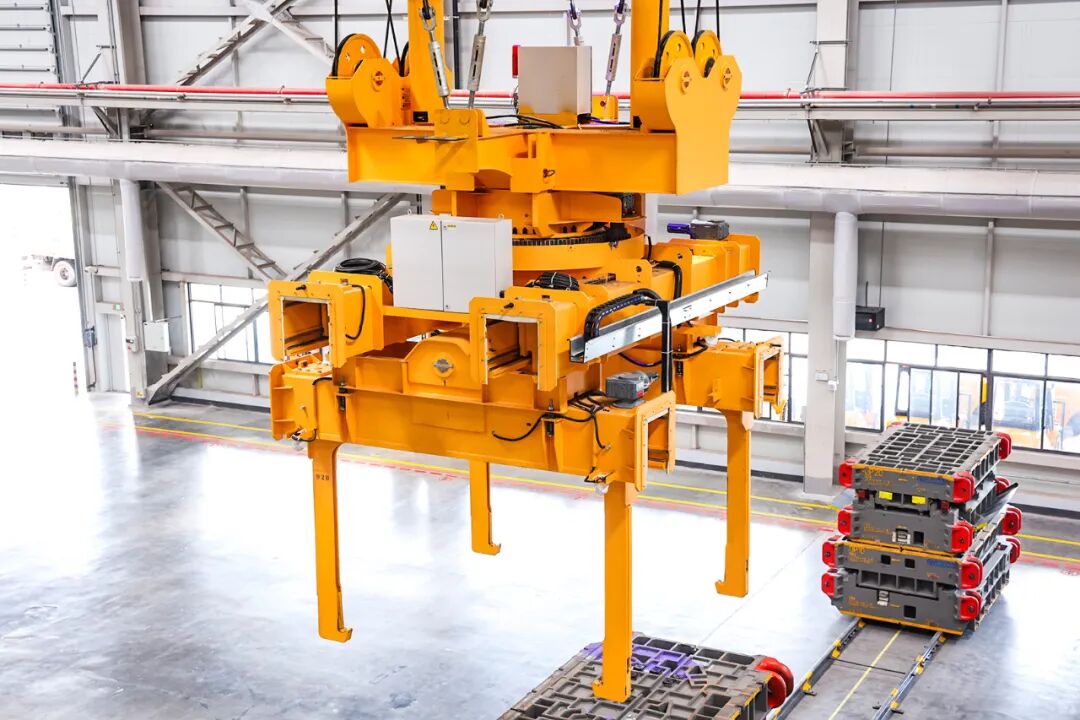
Automated Mould Transfer for an Automotive Stamping Workshop
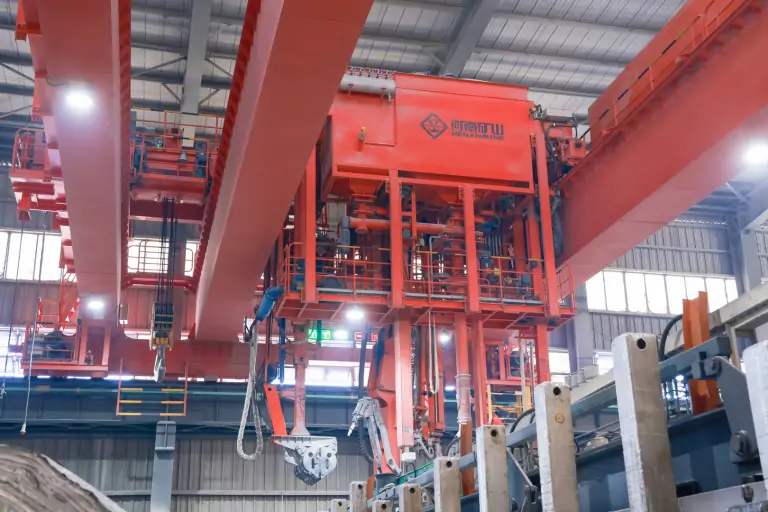
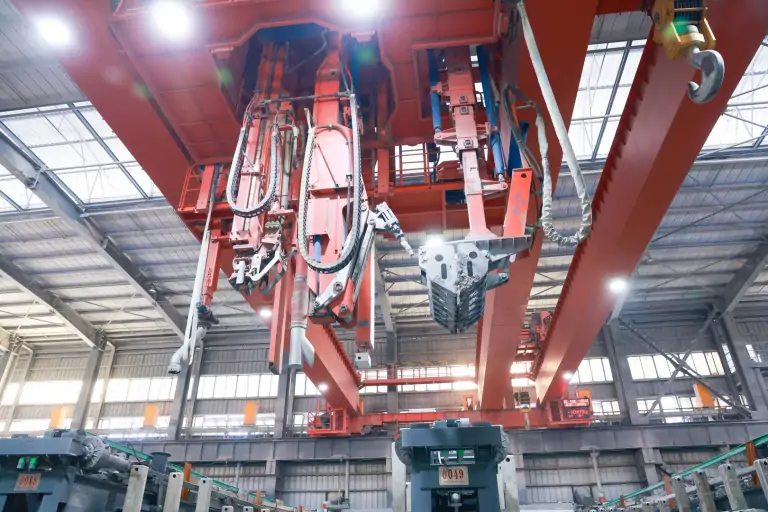
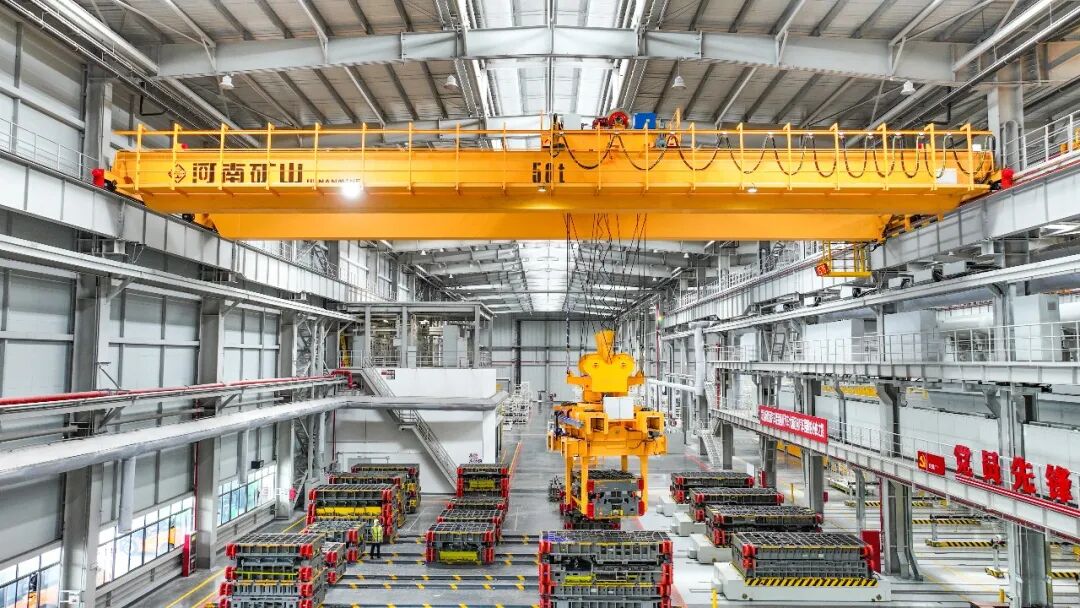
Henan Mine Crane reports delivering a customized automated mould-handling crane for a domestic automotive manufacturer. The published scope identifies automatic positioning, WCS management, area protection, obstacle avoidance, a multidirectional special spreader, anti-sway, servo positioning and three operating modes.
The published safety functions include laser anti-collision, light-curtain area protection, image monitoring and a 3D-vision digital-twin function. The record states that the project was developed for mould transfer in an automotive stamping workshop.
Automotive Industry Crane Price and Budget Scope
An automotive crane cannot be priced accurately from capacity alone. Span, duty, attachment, precision, automation, runway or support structure, line interfaces, local compliance, installation and production acceptance can change the total materially. Public prices reviewed in 2026 illustrate different supply levels and are not equivalent project quotations.
| Public Market Reference | Published Price | Supply Level | Major Scope Boundary |
|---|---|---|---|
| 5 t Bridge Crane Guide Estimate | US$6,000–12,000 | Derived from a published US$1,200–2,400 per tonne crane-only guide | Excludes installation and site construction; no automotive attachment, duty or automation is normalized |
| 5 t Single-Girder Crane Kit with Hoist | US$23,250 | North American component kit listing | Listing includes end trucks, controls, festoon and hoist; bridge steel is sourced locally, with runway and installation outside the stated kit |
| 15 t Cabin-Control Double-Girder Crane Listing | US$55,000–90,000 | Marketplace complete-crane price signal | No normalized span, duty, die attachment, controls, runway, freight, installation or acceptance scope |
| 7.5 t Two-Cell Freestanding Motorized Bridge System | US$94,750.80 | Specific retail system listing, 20 ft wide by 40 ft per cell | A particular support-system layout; automotive tooling, local erection, production interfaces and acceptance remain separate |
| Automated Automotive Die-Handling Crane Project | Project-specific RFQ | Crane, attachment, automation and contracted services | A valid total requires the die database, layout, duty, cycle, positioning, WCS or MES interfaces, safety scope and destination |
Primary Price Drivers
Capacity, span and lift; duty class and speeds; die gripper or lifting device; two-hoist or turning requirement; positioning and anti-sway; automatic controls; WCS, MES and press interfaces; safety zoning; building steel; documentation and local compliance.
Commercial Scope to Reconcile
Runway rails and steelwork; structural reinforcement; freight, insurance, duties and taxes; erection; electrification; commissioning; test loads; representative dies; line-interface testing; training; spares; warranty and production acceptance.
Engineering and Procurement Deliverables
A procurement-ready offer defines measurable performance, interfaces, evidence and commercial boundaries.
Technical Proposal
Design basis, crane arrangement, capacities, classification, speeds, attachment, load assumptions, precision, protection package, operating modes and stated deviations.
Interface Schedule
Runway reactions, power, communications, press and station I/O, coordinates, safety ownership, erection needs, civil boundaries and third-party responsibilities.
Attachment Documentation
Rated range, deadweight, dimensions, engagement, locking logic, proof test, inspection limits, wear parts, attachment stand and representative-load acceptance plan.
Safety and Controls
Risk-assessment inputs, safety-function list, restricted zones, interlock matrix, network behavior, isolation, emergency states, recovery and required conformity records.
Quality and O&M Records
Inspection and test plan, material and welding records as specified, coating reports, component certificates, manuals, lubrication plan, training and critical spares.
Commercial Schedule
Price, Incoterm, milestones, packing, freight boundary, installation, commissioning, training, acceptance, warranty, exclusions, validity and optional lifecycle services.
Automotive Industry Crane RFQ Information
The following data supports a configuration-based technical and commercial proposal.
Load and Attachment Data
Load families; minimum and maximum mass; dimensions; center of gravity; lifting points; orientation; surface restrictions; photographs or drawings; proposed gripper, beam, tong, C-hook, vacuum device or rigging.
Process and Duty Data
Source and destination stations; changeover sequence; lifts per hour; shifts; annual hours; load spectrum; travel distance; target cycle; placement tolerance; availability and contingency.
Site and Environment Data
Span, lift, runway length, building and process drawings, allowable reactions, press and rack interfaces, temperature, dust, welding, paint, clean or dry-room requirements, power and destination.
Controls and Commercial Data
Operating modes; WCS, MES and PLC protocols; task and die identity; safety zones; governing standards; Incoterm; freight, installation, commissioning, test and documentation boundaries.
Frequently Asked Questions
Which crane is used in an automotive press shop?
A process-duty double-girder overhead crane is commonly selected for heavy die storage and changeover. A dedicated die gripper, anti-sway, precision motion and press-line interfaces may be added when cycle frequency and automation justify them.
Is one crane suitable for the entire automotive plant?
Usually not. Press dies, body fixtures, powertrain components, assembly tasks and maintenance loads differ in mass, frequency, precision and environment. A plant-wide lifting plan assigns a suitable crane class to each zone.
How is die-handling crane capacity determined?
Capacity covers the heaviest die plus the complete gripper, beam or other below-the-hook device. Center of gravity, load share, acceleration, turning requirements and governing code are then applied.
Can the crane retrieve dies automatically?
Yes. Automatic retrieval can combine a die database, WCS tasks, position tracking, a dedicated gripper, anti-sway, protected zones and press handshakes. Safe exception handling and manual recovery remain mandatory design elements.
Does an automotive crane need millimetre-level positioning?
Only where the actual station and attachment require it. The purchase specification defines the measurement point, load, speed, repeatability and acceptance method rather than using an unsupported general accuracy claim.
Are explosion-proof cranes required in paint shops?
Only when the approved hazardous-area classification establishes the relevant zone and protection requirements. Solvent use or a paint-shop label alone does not determine the final crane certification.
How much does an automotive industry crane cost?
Public figures range from crane-only estimates and component kits to complete support systems. A defensible project price requires capacity, span, duty, attachment, automation, plant interfaces, building scope, destination and acceptance criteria.
Can an existing runway be reused?
Only after geometry, condition, fatigue history, rails, beams, columns, connections and foundations are verified against the proposed vertical, lateral, longitudinal and buffer reactions.
Related Automotive Industry Crane Products
Select the crane platform according to the load, working area, building structure, duty cycle, positioning requirement and production interface.
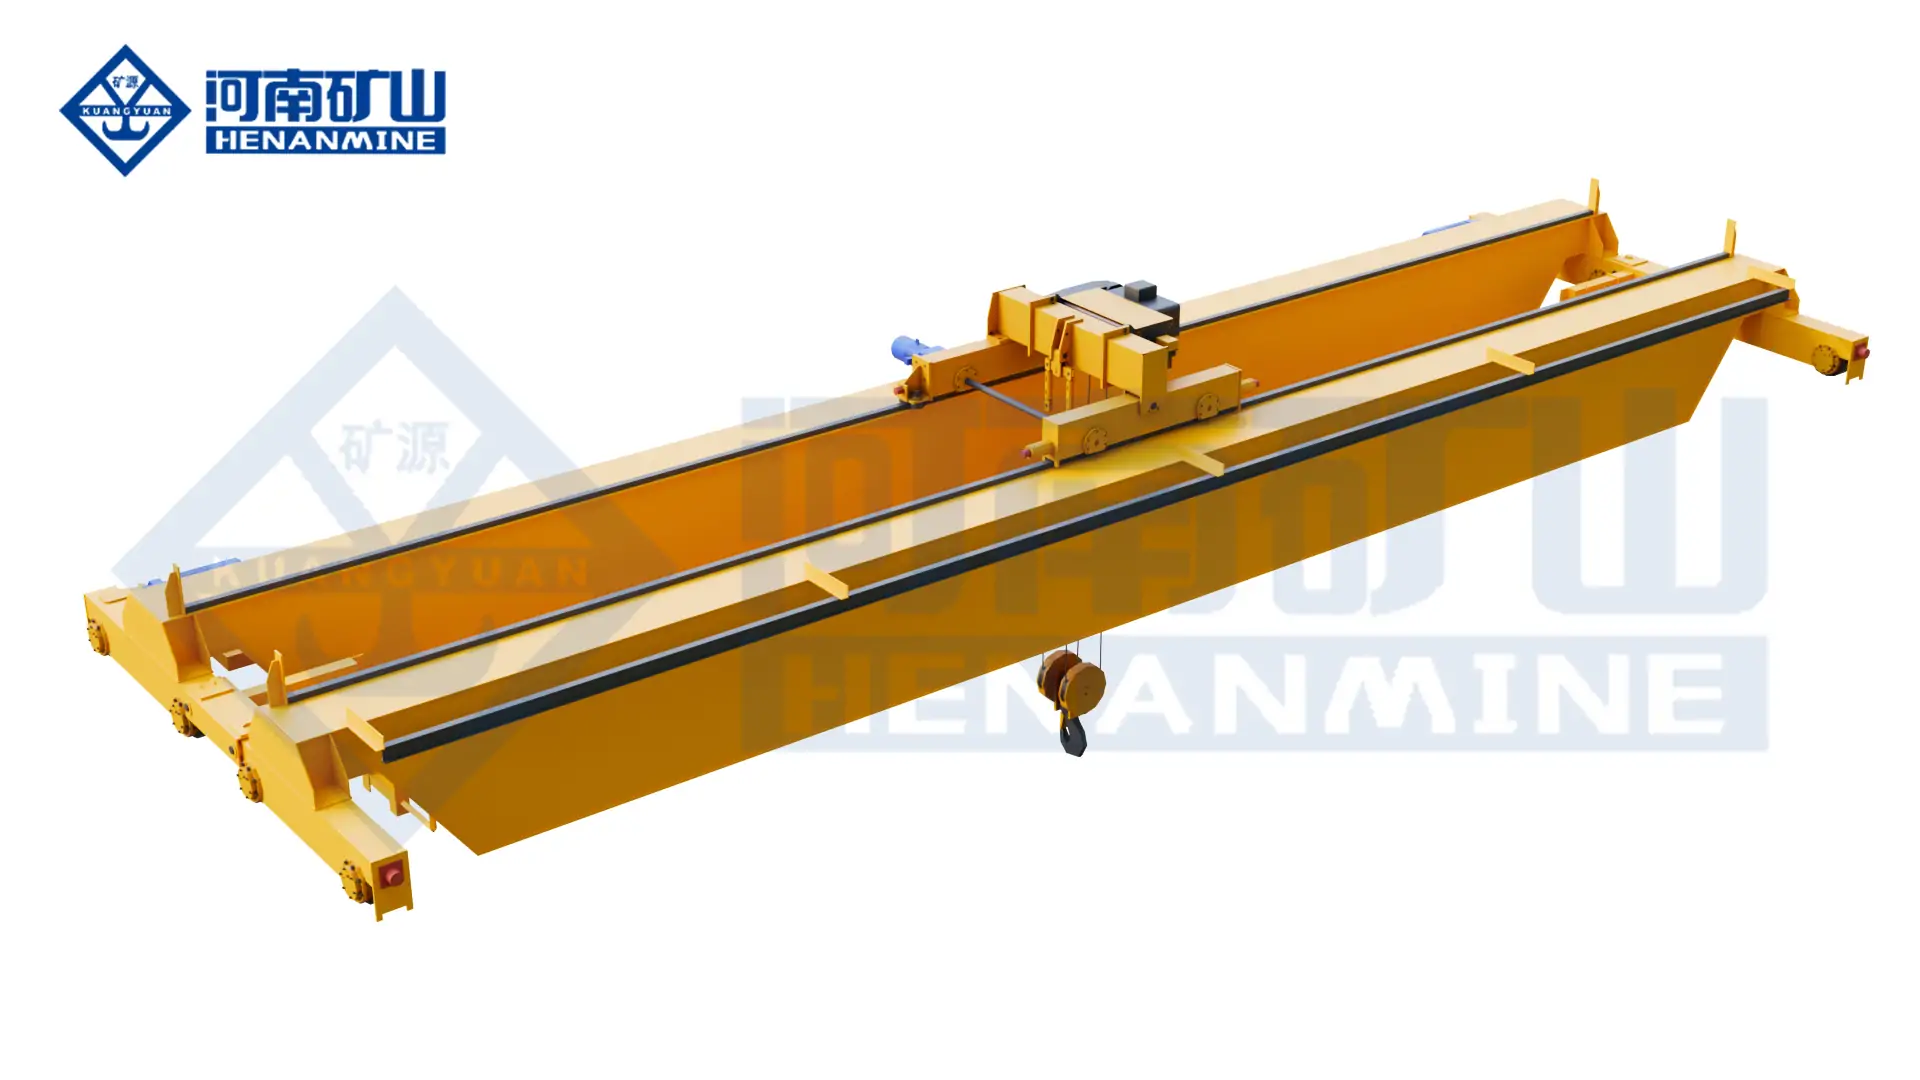
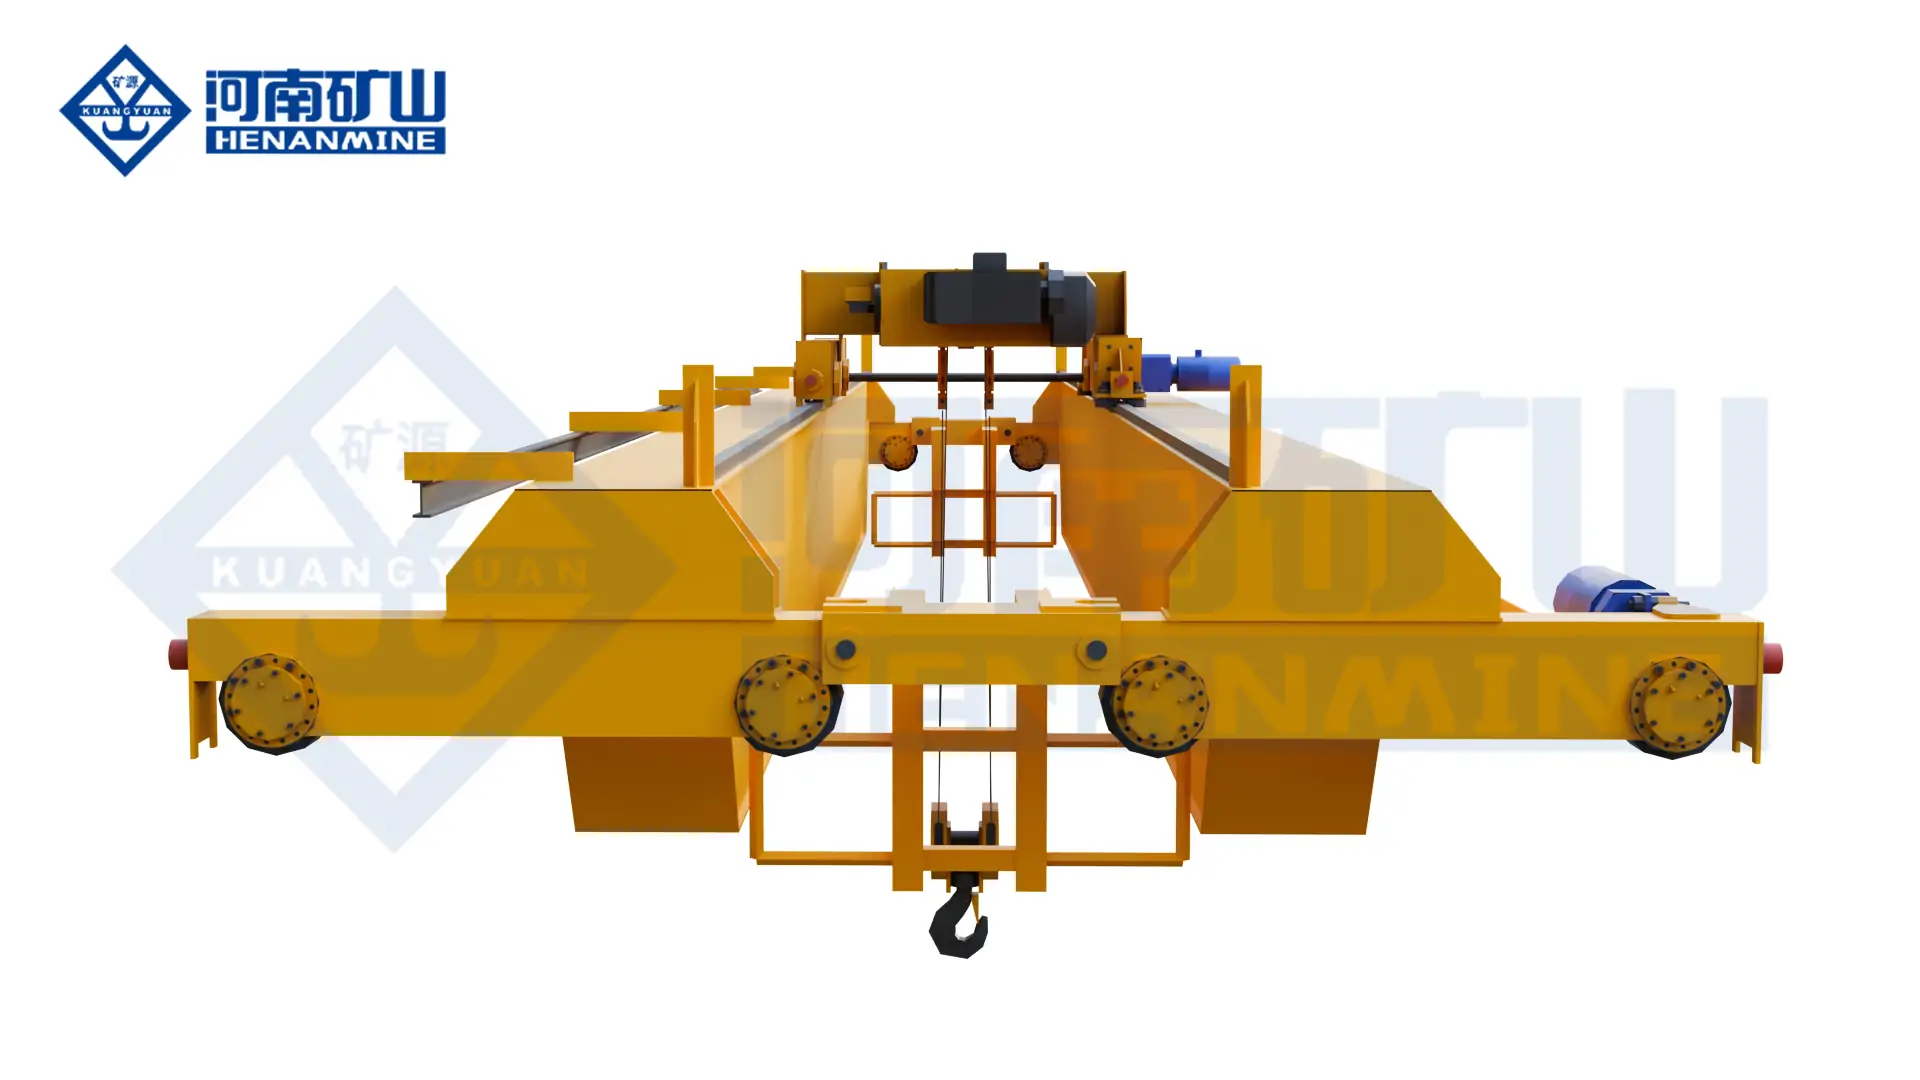
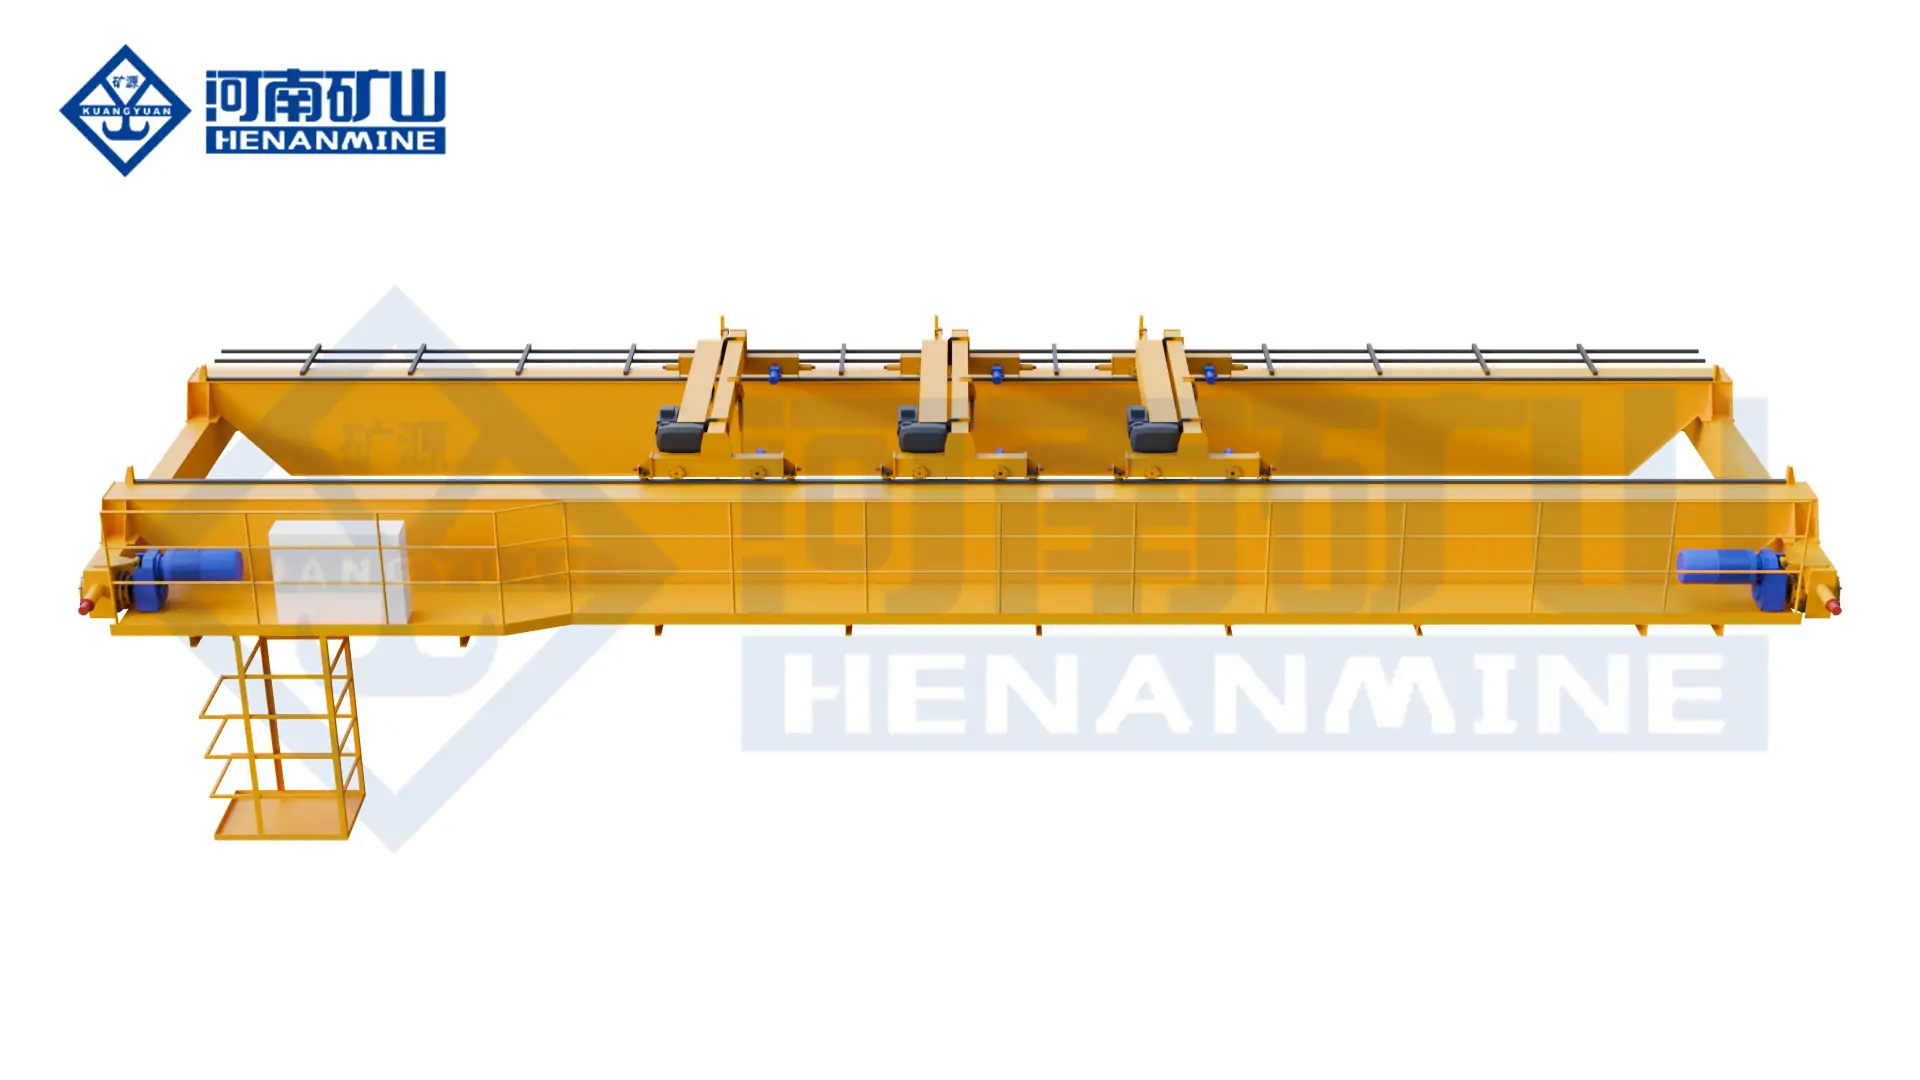
Double-Girder Bridge Crane
Heavy-duty overhead platform for press dies, large fixtures, tooling and maintenance loads.
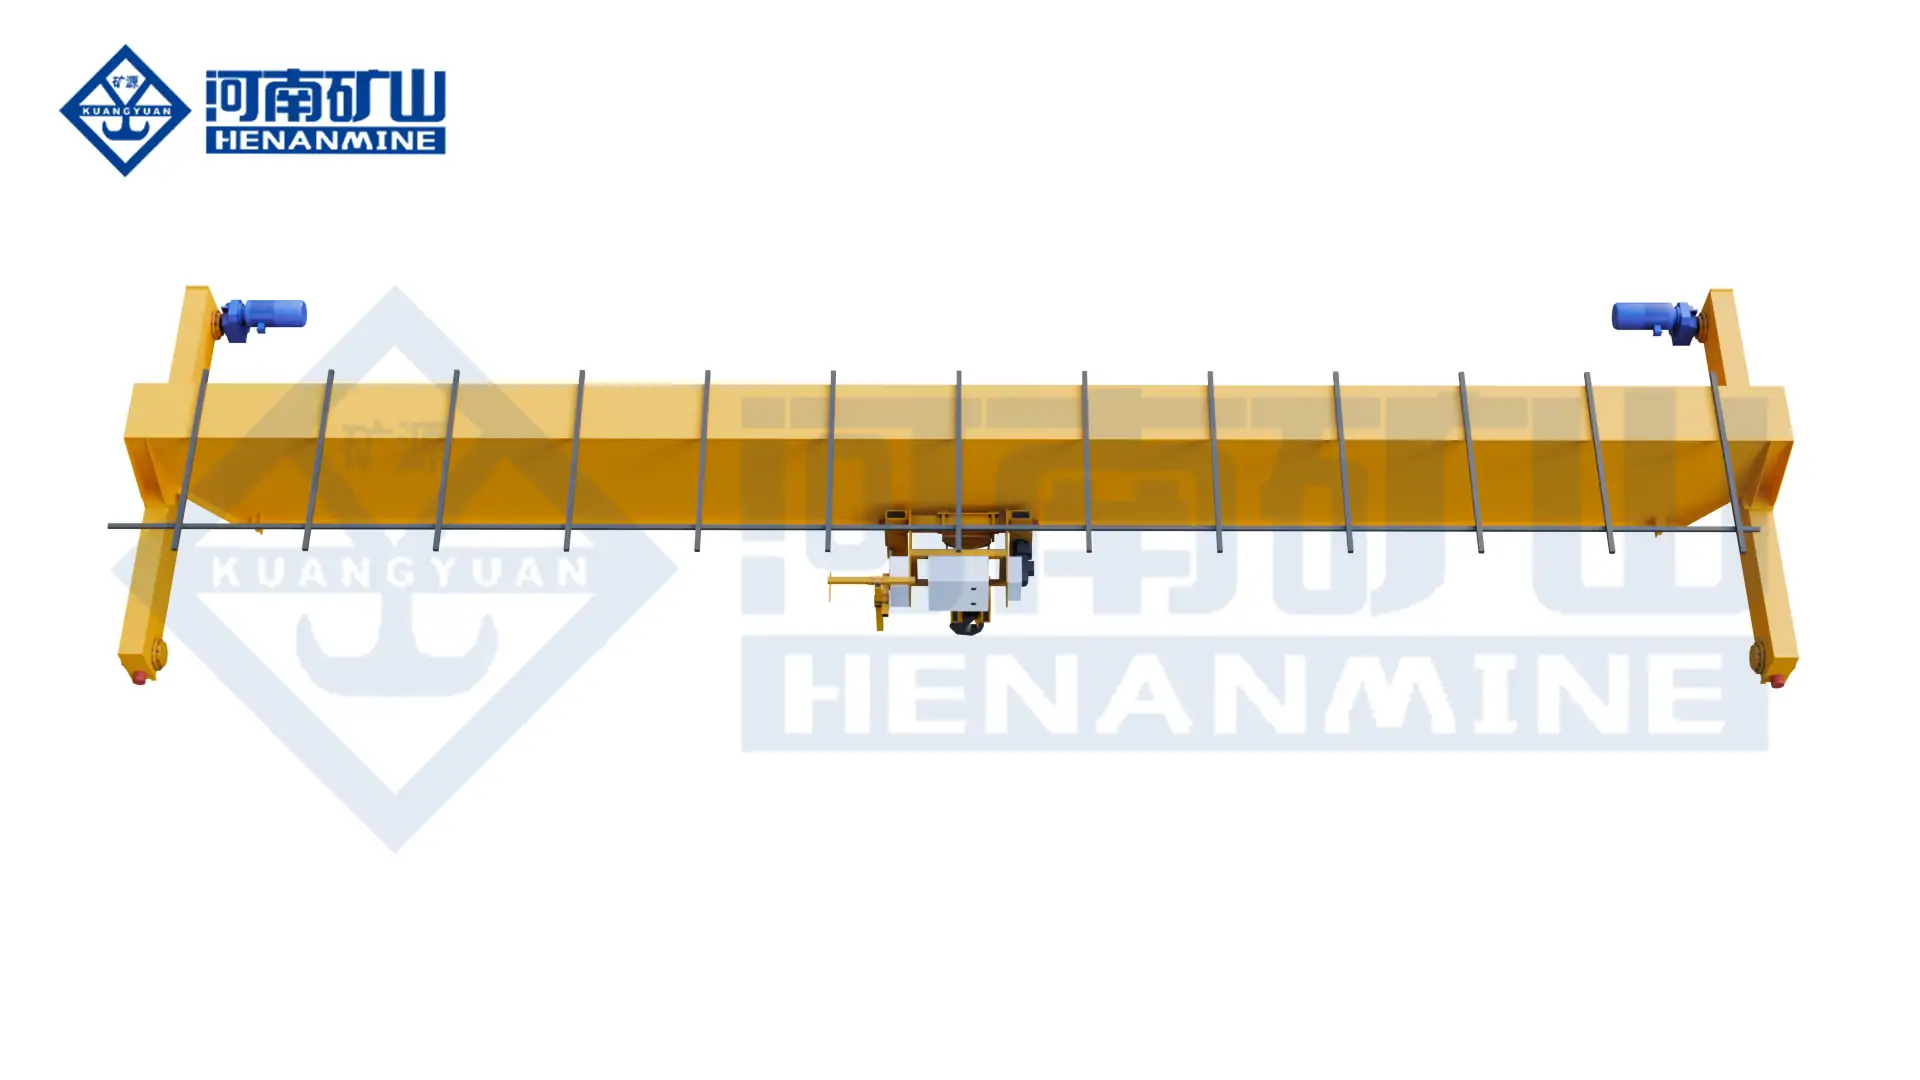
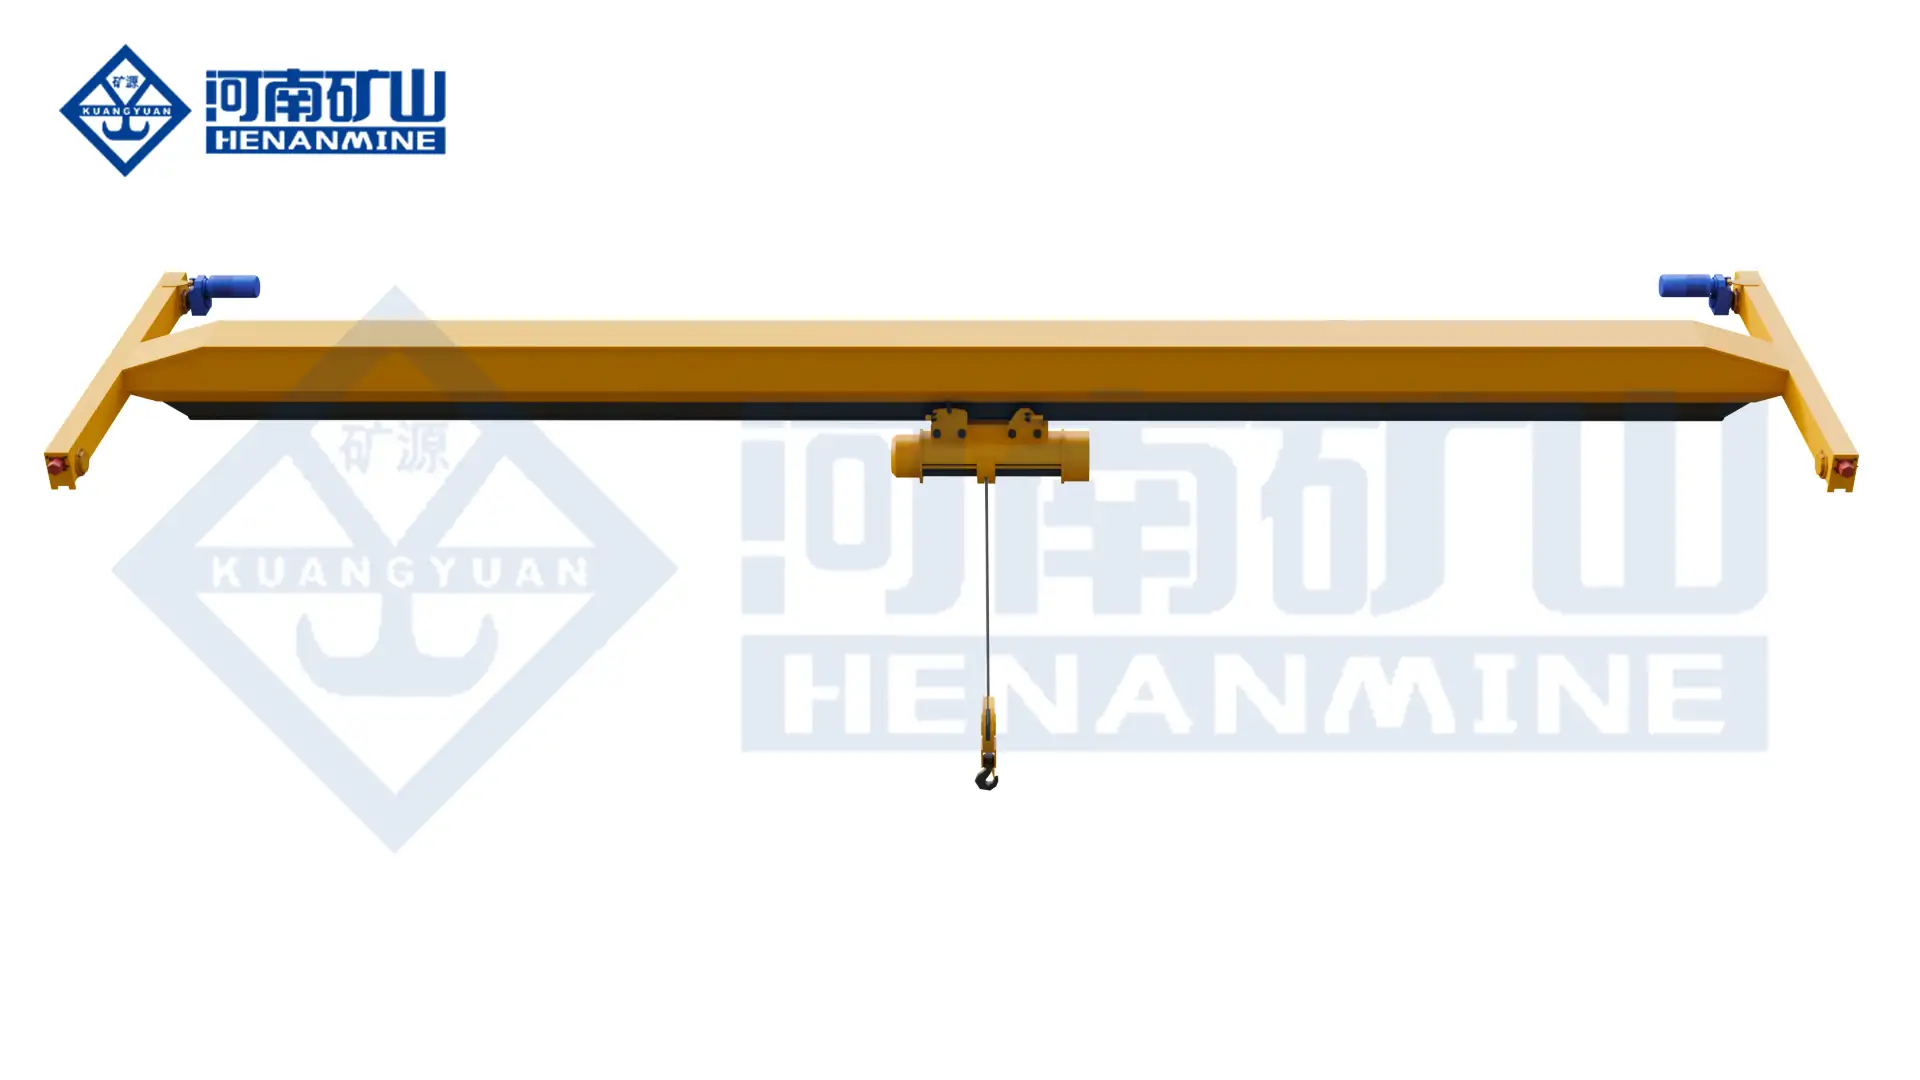
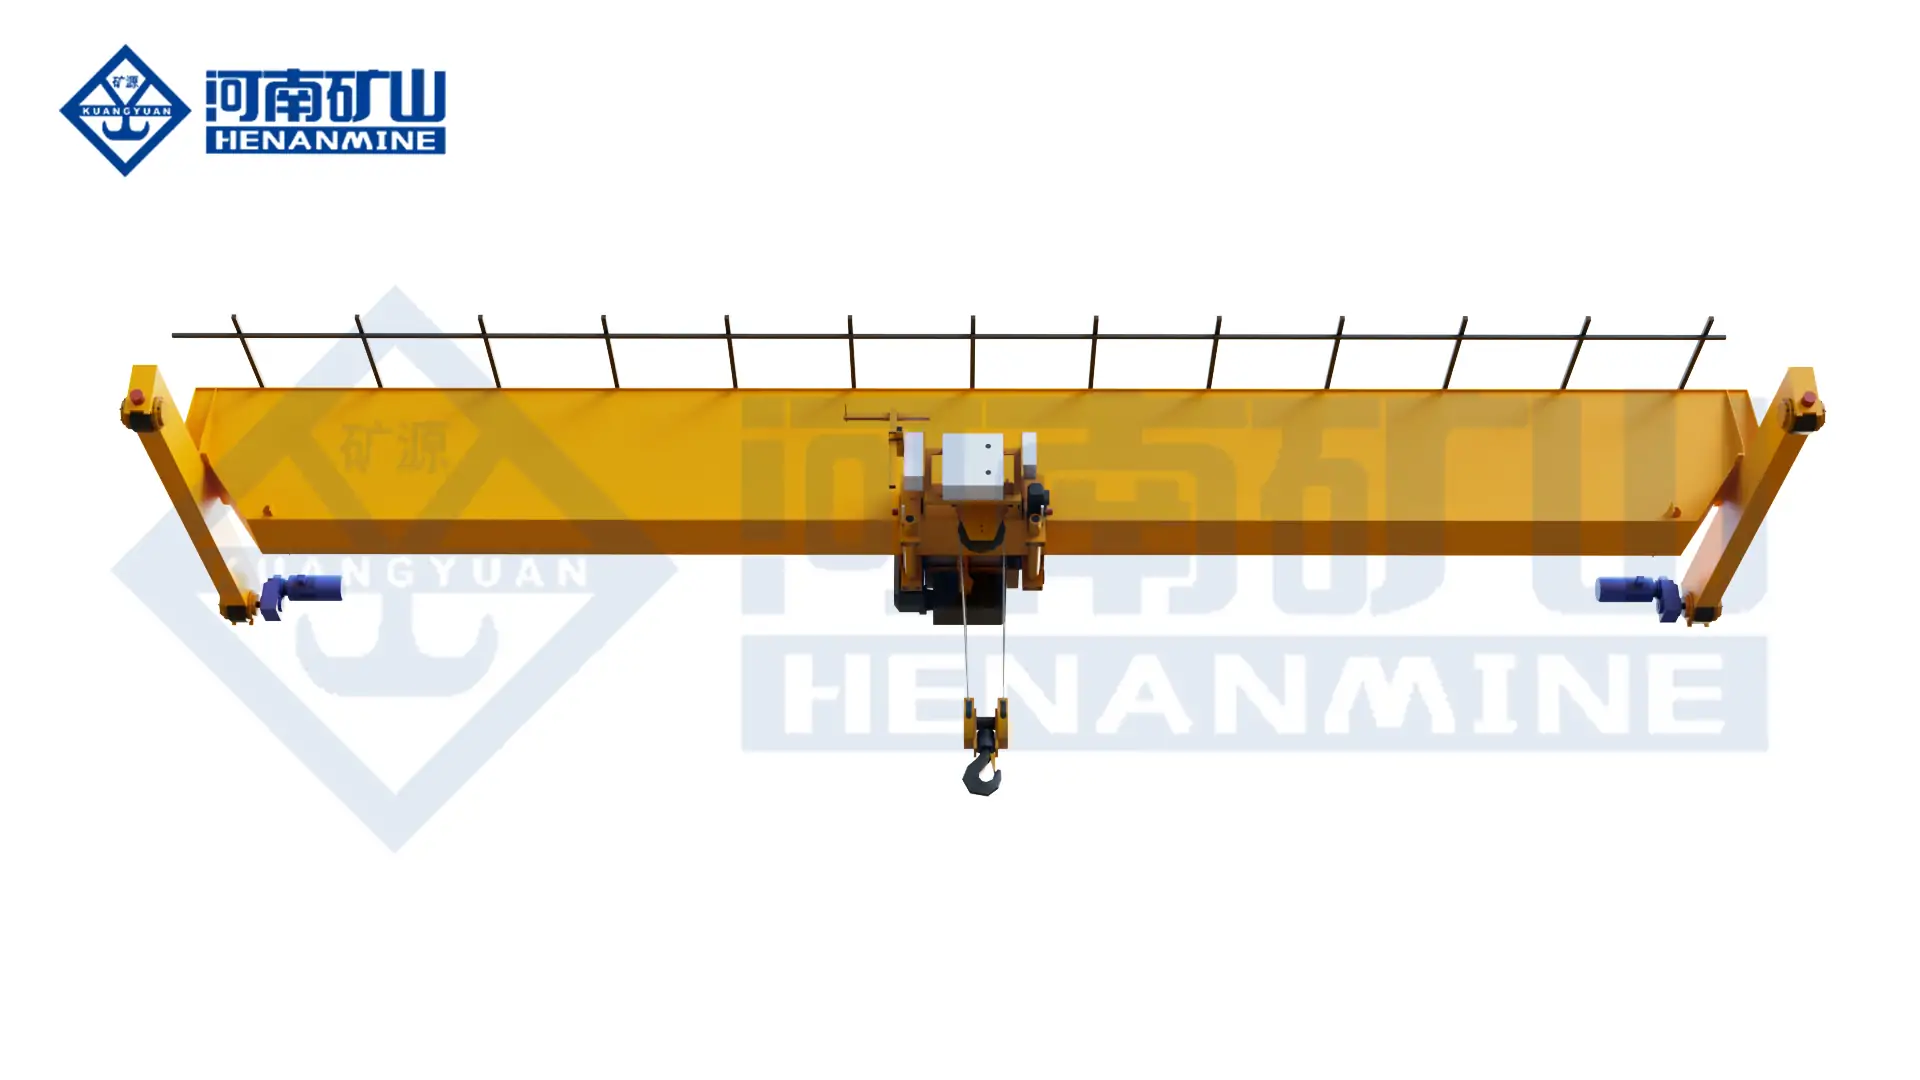
European-Style Electric Single-Girder Crane
Compact crane for automotive components, tooling, warehouses and planned line maintenance.
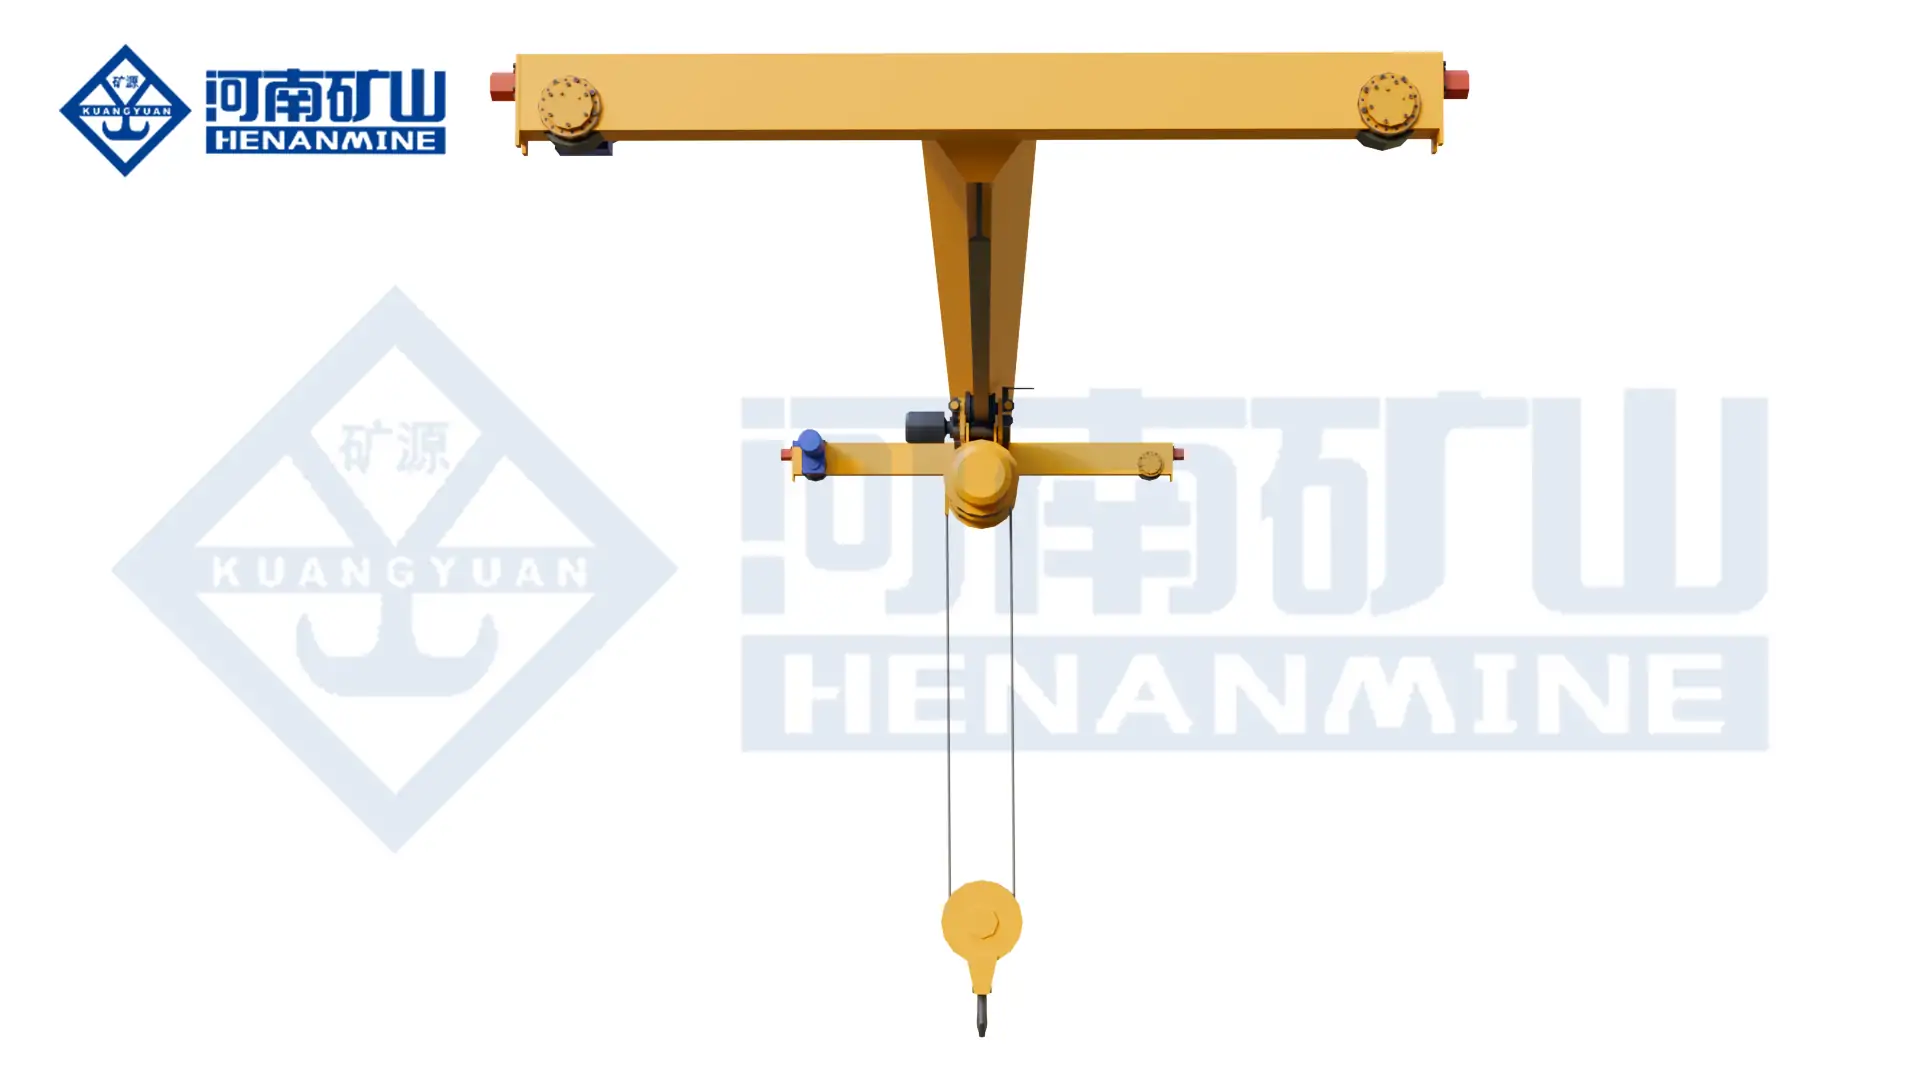
Single-Girder Suspension Crane
Underhung coverage for body, assembly and maintenance areas with suitable roof support.
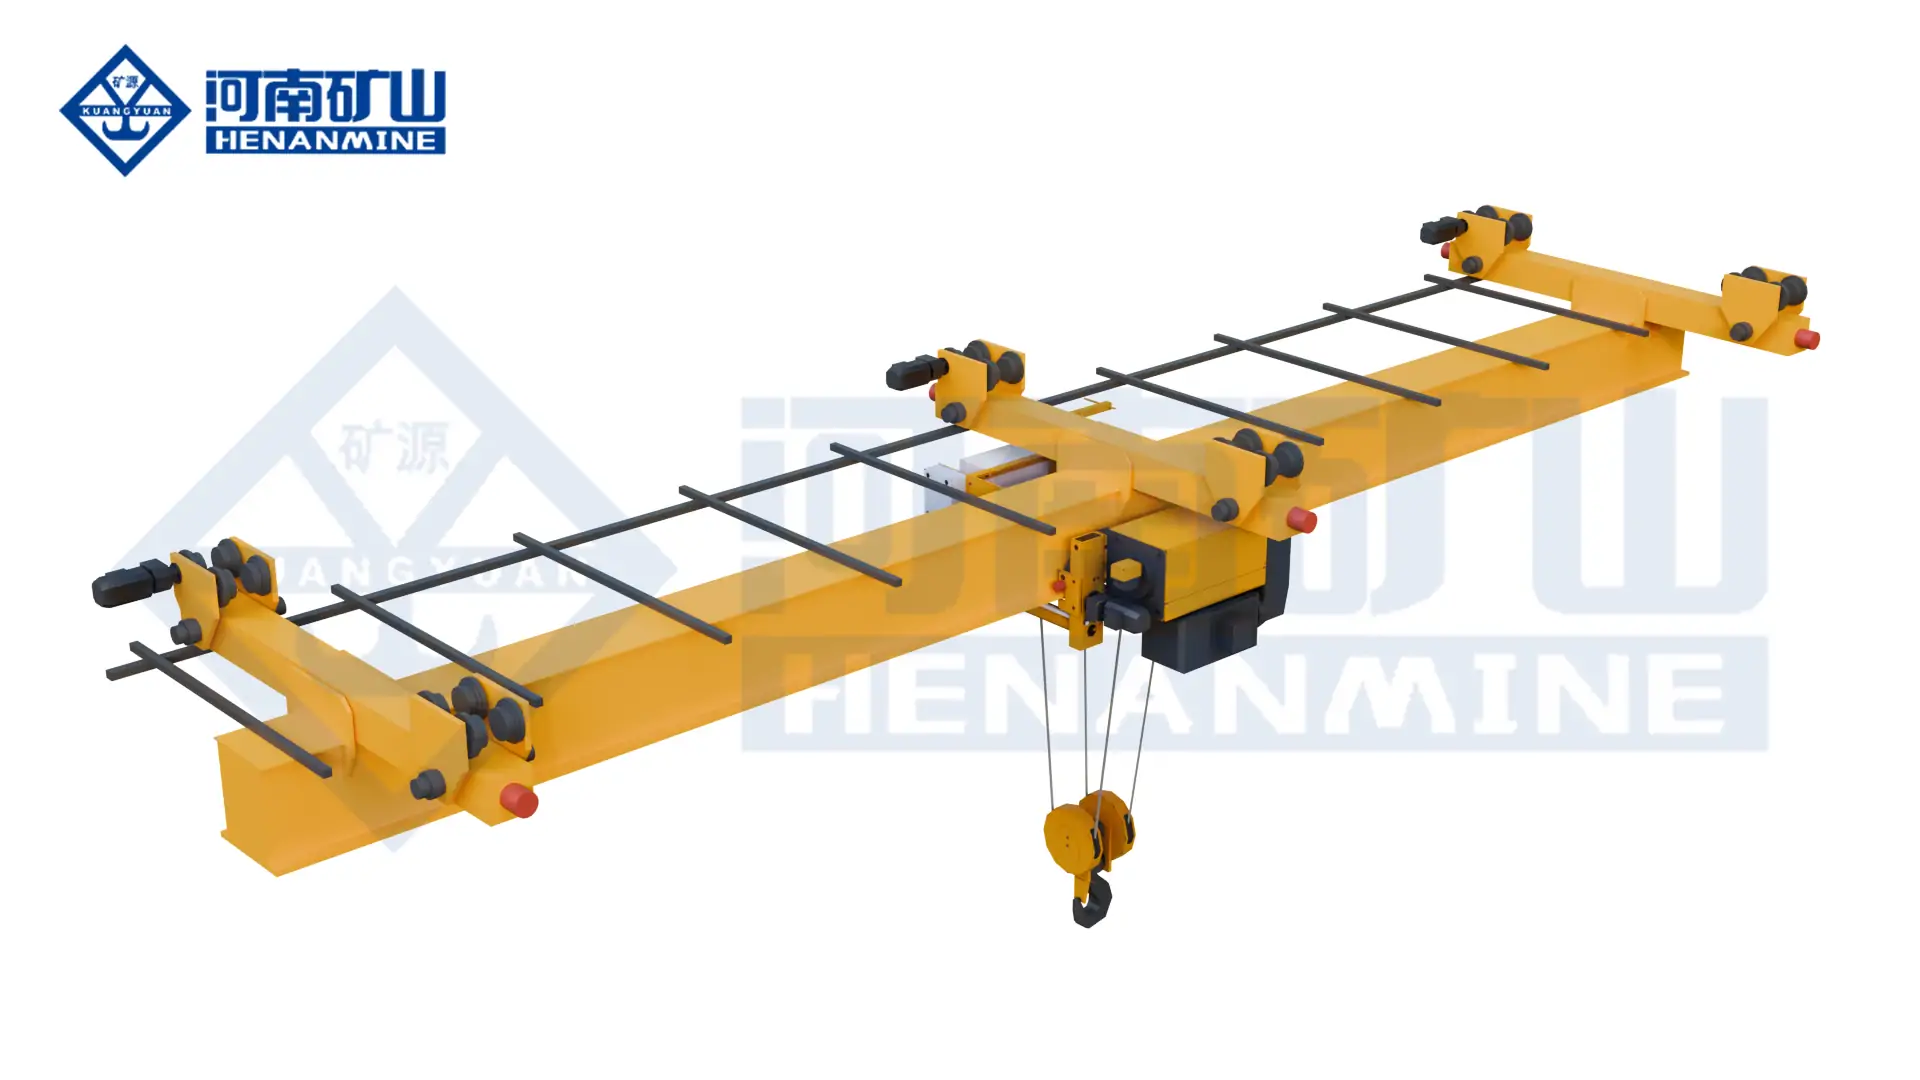
Single-Girder Overhead Crane
Top-running bridge crane for general component handling, tooling support and workshop service.
Intelligent Electric-Hoist Crane
Low-headroom electric-hoist platform with controlled-motion and digital monitoring options.
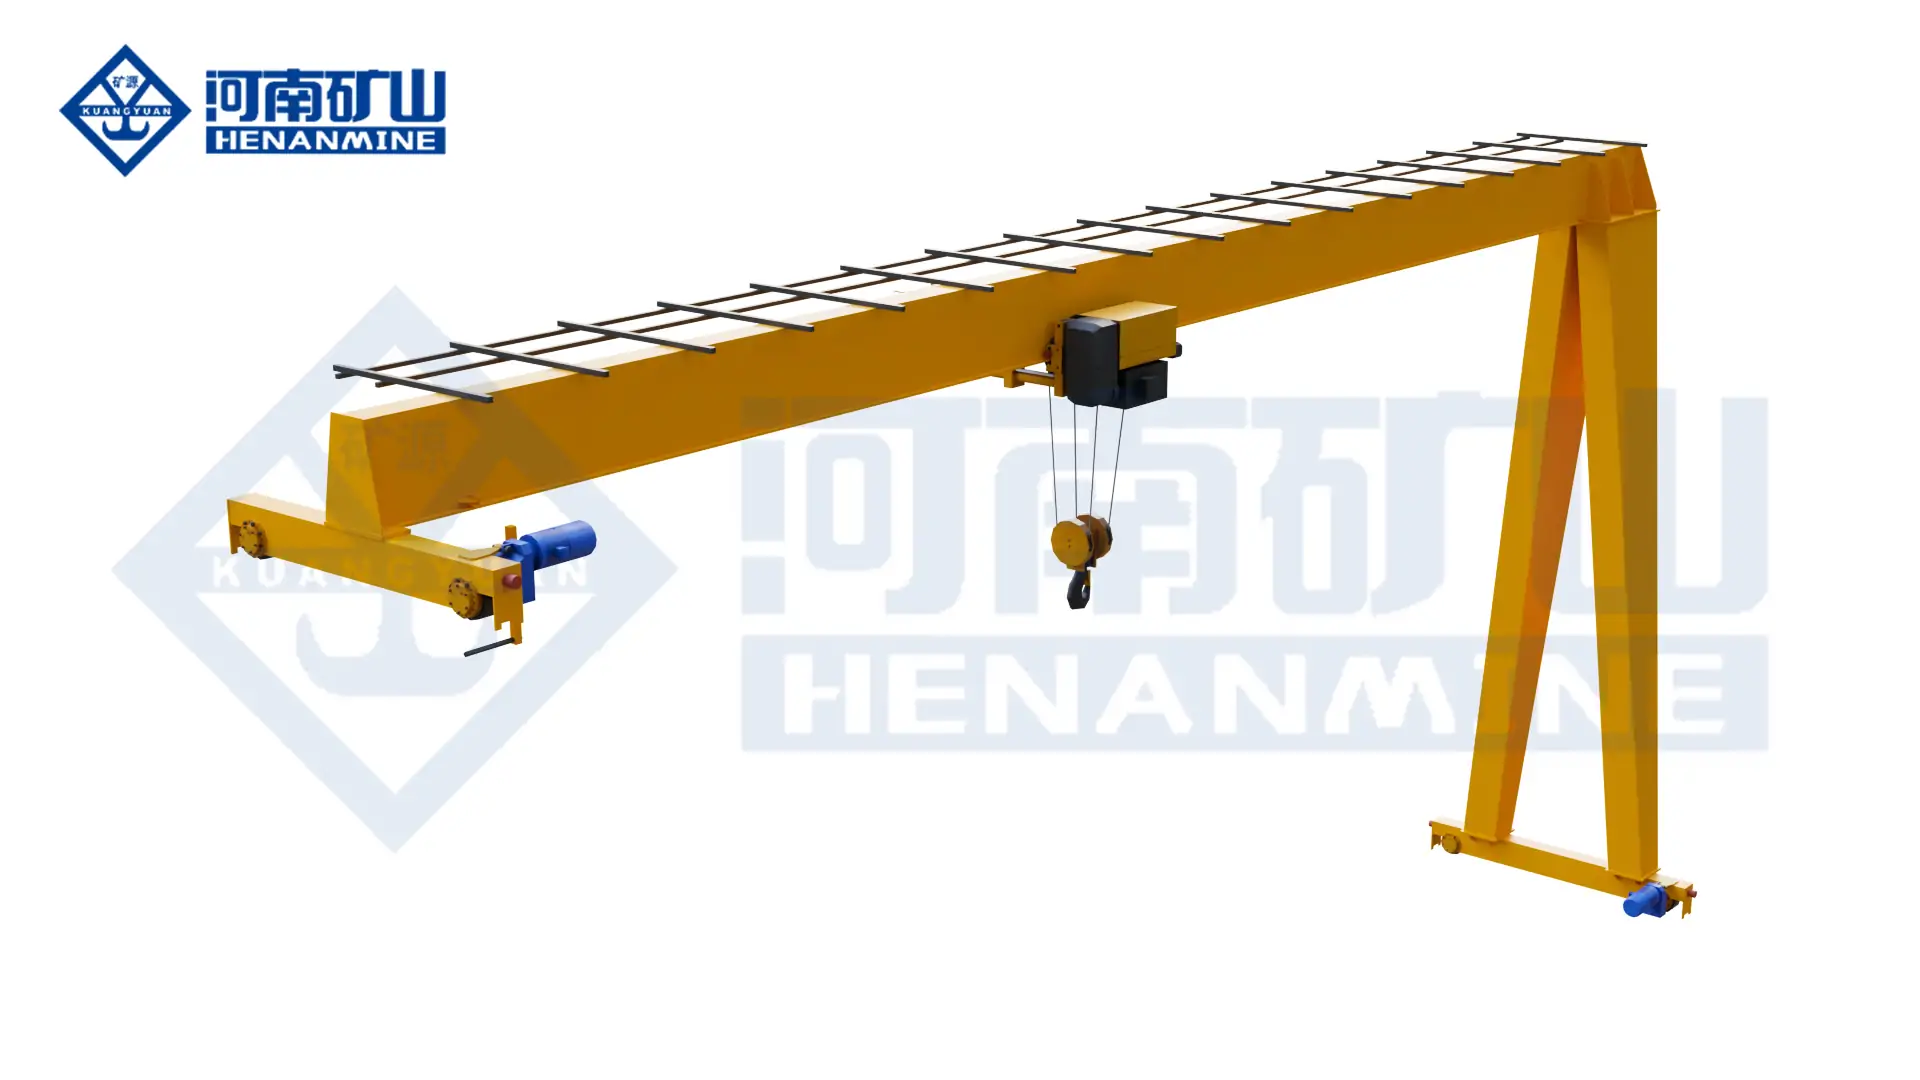
Semi-Gantry Crane
Localized handling for loading edges, workshop extensions and production-support zones.
Request an Automotive Industry Crane Quote
Submit the load or die schedule, attachment concept, handling sequence, cycle and positioning requirements, span, lift, runway and plant drawings, operating environment, control level, WCS or MES interfaces, safety zones, power supply, project destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.