分类: Selection Guides

Equipment selection by lifting capacity, technology and working environment.

  • Waste to Energy Crane

    Waste to Energy Crane

    Waste to Energy Crane

    WASTE BUNKER HANDLING · MIXING · FURNACE FEEDING

    Waste to Energy Crane

    Henan Mine Crane supplies engineered grab overhead cranes for waste reception, bunker mixing and furnace feeding at waste-to-energy plants.

    The furnace needs a steady waste supply while the crane also clears the tipping area and mixes the bunker. We bring the crane, grab and controls into one proposal, with handling capacity calculated for the complete working cycle.

    Request a Waste Crane Proposal
    View Our WTE Project

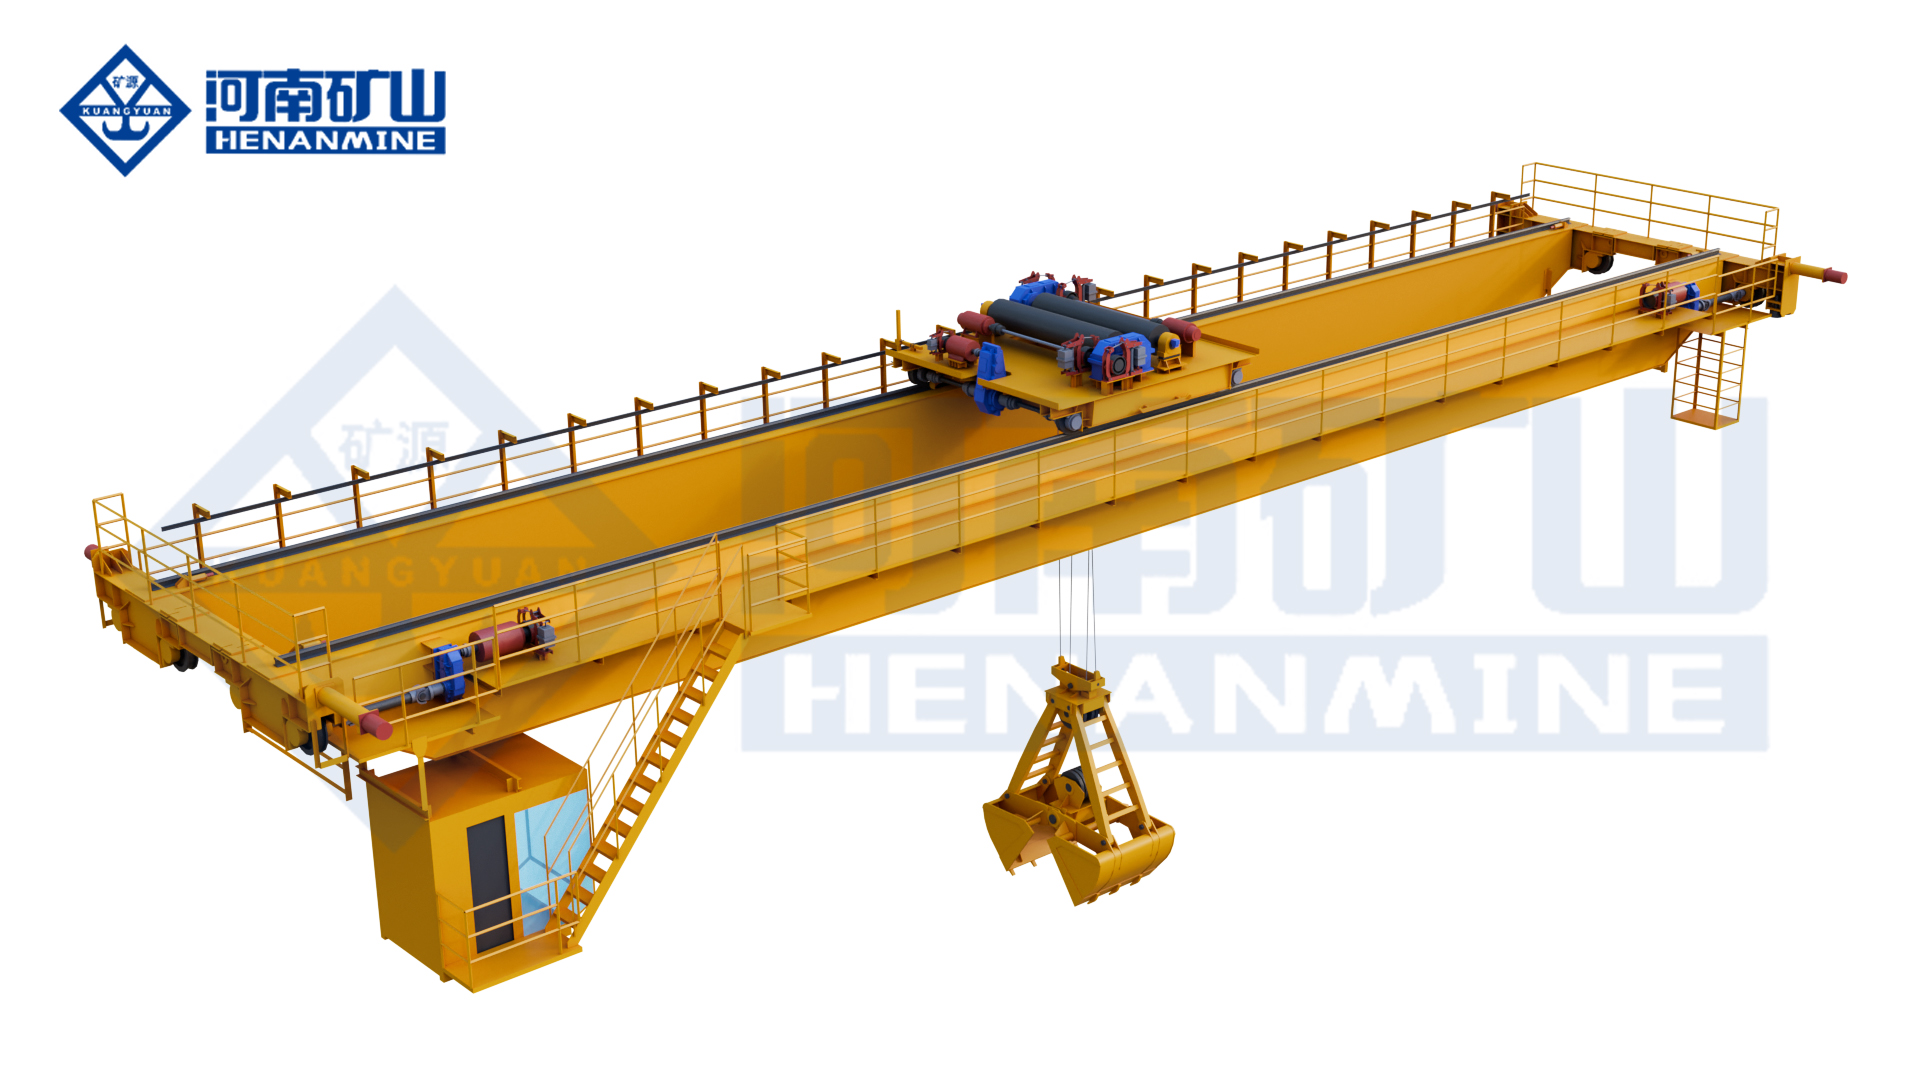
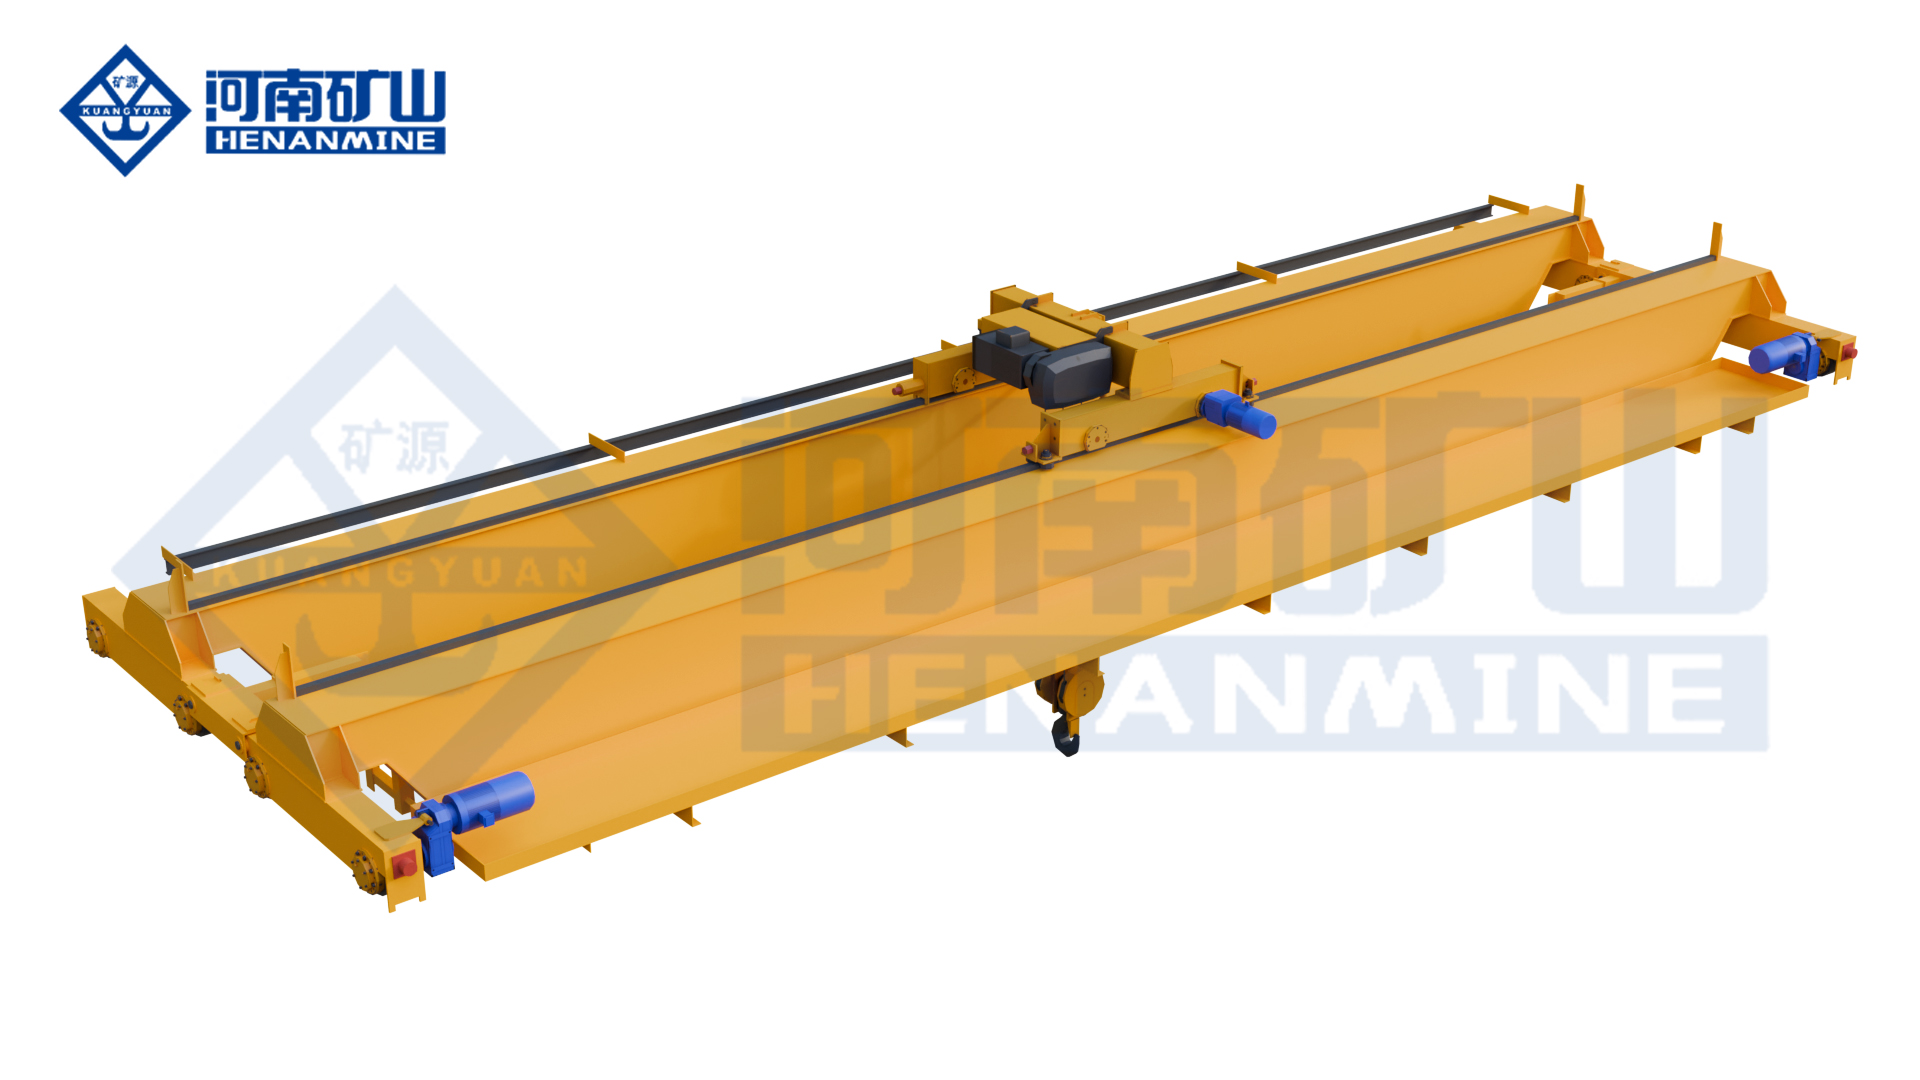
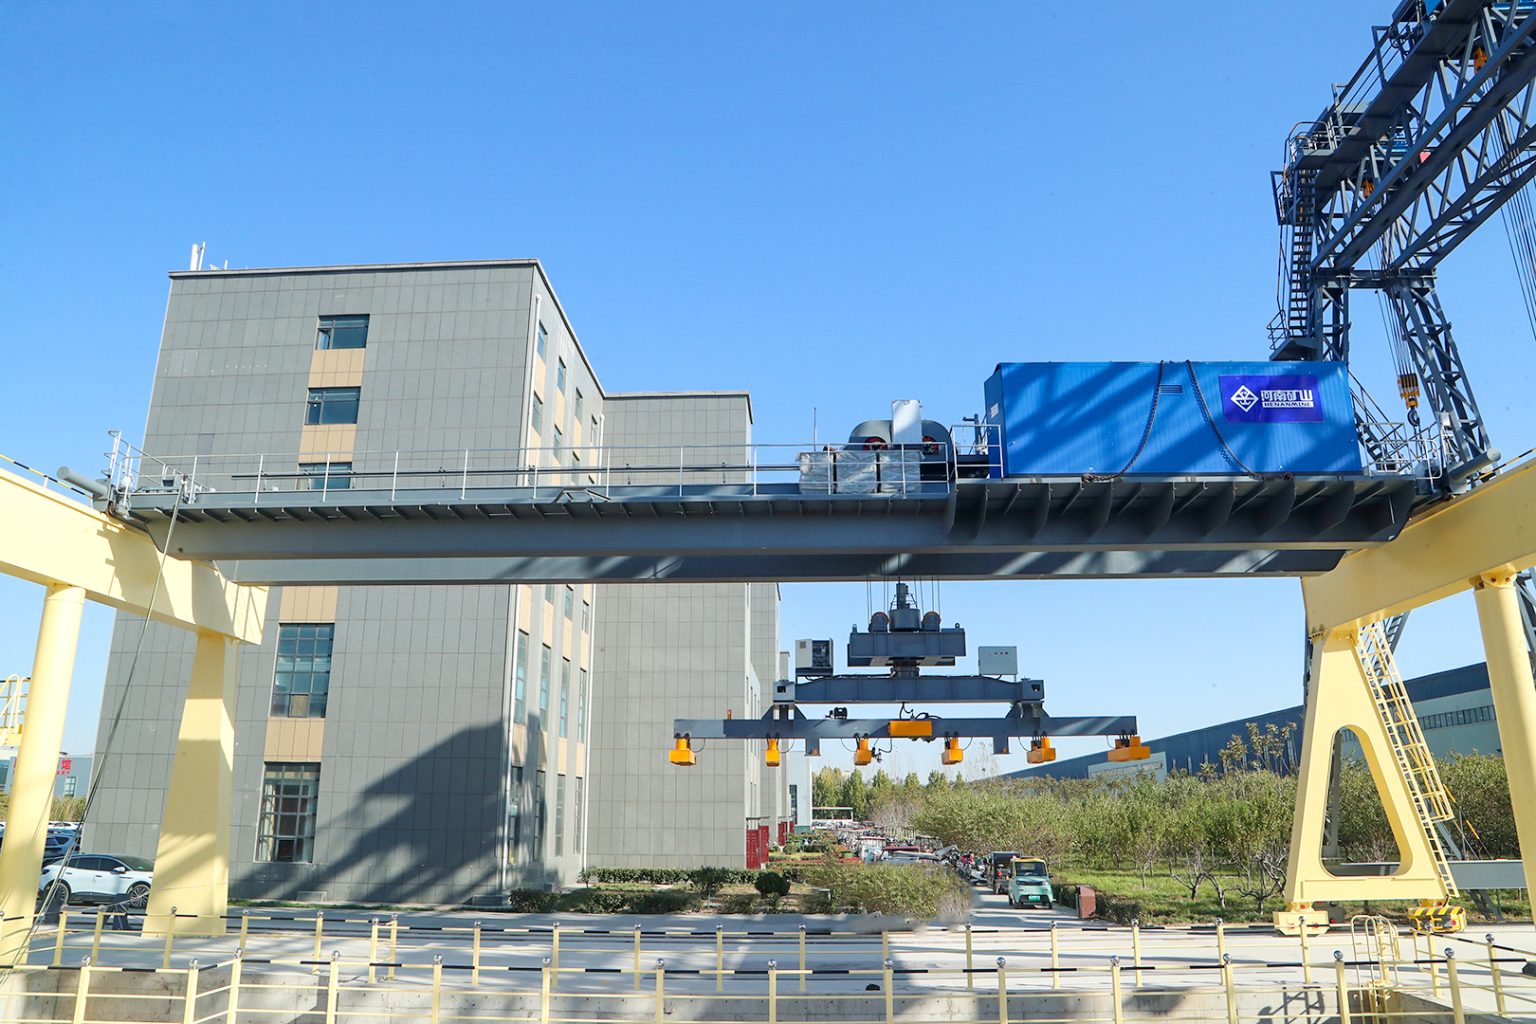
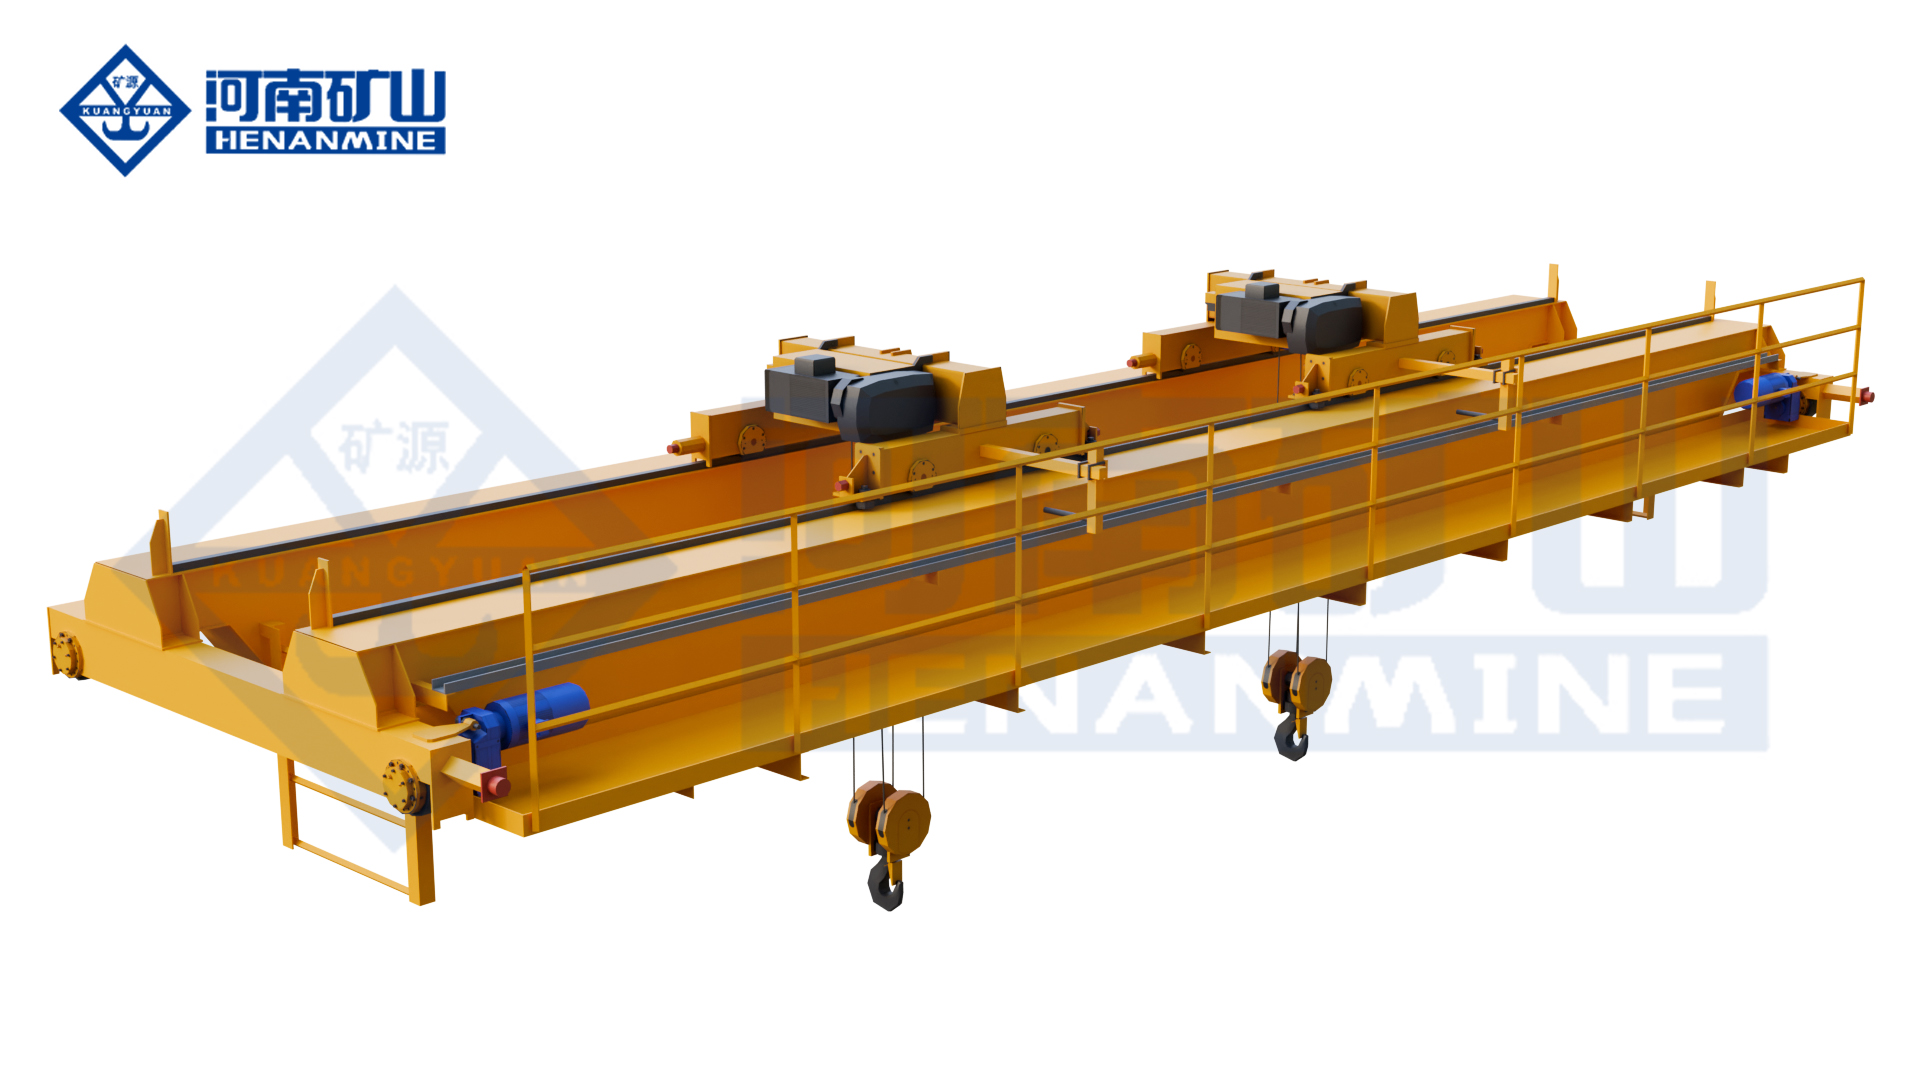
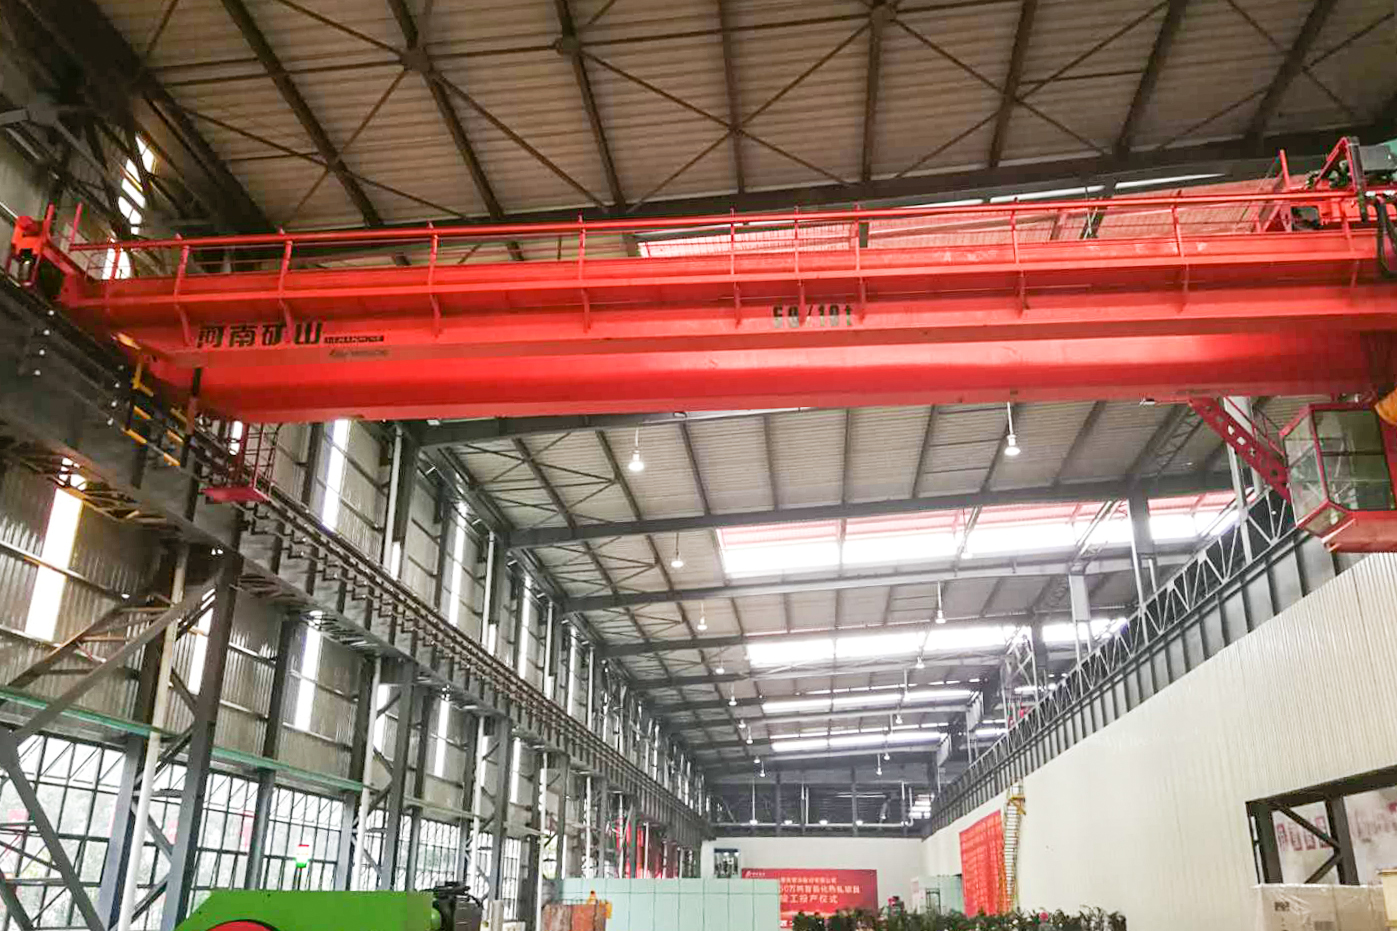
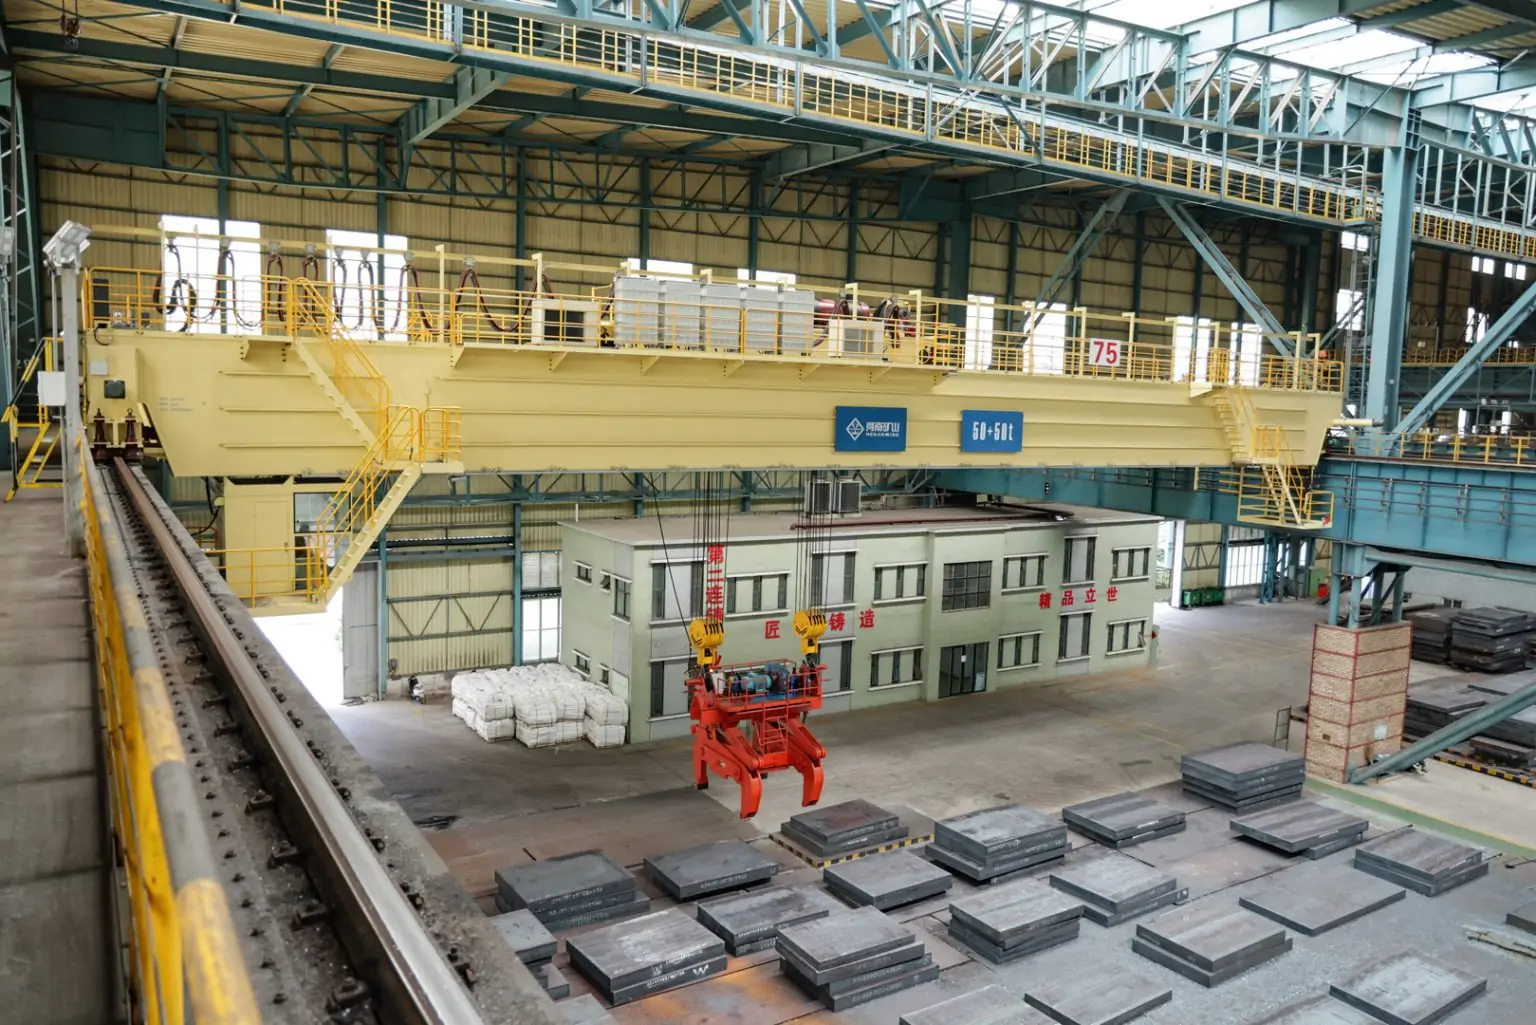
    Henan Mine Crane intelligent grab overhead crane product platform
    Intelligent grab crane product platform. The waste grab and final arrangement are selected for the plant duty.

    A Waste Handling Package from One Crane Manufacturer

    Crane, grab and controls

    We propose the bridge, trolley, waste grab, power supply and control system together. The technical offer defines what is included and how the equipment connects to the bunker and feed hoppers.

    Engineering around furnace demand

    Our selection considers waste payload, cycle time, mixing and transfer work. You receive an equipment arrangement and operating basis that can be checked against the plant’s required handling rate.

    Support through commissioning

    Installation guidance, commissioning assistance, operator training and spare-parts support can be included. The quotation separates equipment supply from site services, so the project team can budget both.

    Our practical advantage: Henan Mine Crane has a published, commissioned automatic grab crane reference in waste incineration power generation. That experience provides a concrete starting point for discussing control functions and the proposed operating sequence.

    What a Waste to Energy Crane Does

    A waste to energy crane, also called a waste bunker crane or garbage grab crane, moves municipal solid waste inside the storage bunker and delivers it to incinerator feed hoppers. Its workload includes more than furnace feeding.

    Bunker task What the crane arrangement provides
    Clear the reception area Transfer newly delivered waste away from tipping positions to keep the receiving area usable.
    Mix and redistribute waste Move waste between bunker zones to blend incoming material and manage the stored pile.
    Feed the furnace hoppers Carry waste to designated discharge points, with controlled approach and hopper-ready interlocks where included.
    Record handled loads A weighing option can record loads and feeding totals, with the measurement method and calibration procedure stated in the offer.

    For plant operators, the key result is enough handling capacity to perform these tasks while maintaining the agreed feeding schedule. Crane tonnage alone does not describe that capacity.

    Select the Crane and Waste Grab Together

    For a building-mounted waste bunker, a dedicated double-girder grab overhead crane is the usual starting arrangement. We select the grab geometry, lifting machinery and travel system around the waste and bunker layout.

    Plant condition Equipment approach
    Mixed municipal waste with bulky or irregular pieces Evaluate a multi-tine or orange-peel waste grab, including penetration, closure, retention and maintenance access.
    A more uniform bulk stream Compare grab geometries against the actual material. A clamshell suitable for coal or sand is not automatically suitable for mixed refuse.
    Frequent mixing and repeated furnace feeding Select the mechanisms and duty classification from the expected load spectrum and operating cycles.
    An existing bunker and runway Develop the replacement layout around rail spacing, wheel reactions, building clearance and hopper reach.
    A phased automation project Offer the initial operating modes and separately identify sensors, plant interfaces and functions for a later upgrade.

    Compare the Main Handling Arrangements

    Arrangement Best procurement fit Important distinction
    Dedicated waste grab overhead crane Bunker mixing, transfer and repeated incinerator feeding. Grab performance, complete-cycle throughput and continuous service duty drive the design.
    General-purpose grab overhead crane Defined bulk streams such as coal, ore or other process materials. Waste compatibility and severe-duty requirements require a separate review.
    Grab-and-hook overhead crane Areas combining occasional bulk handling with equipment lifting. Attachment flexibility does not establish suitability for continuous furnace feeding.
    Electric-hoist overhead crane Workshop and equipment-maintenance lifting. This is a separate maintenance duty from waste bunker handling.
    Grab-and-hook gantry crane Suitable outdoor auxiliary material handling areas. Ground rails, weather conditions and material compatibility determine suitability.

    Technical Schedule for Your Offered Crane

    The final specification identifies the crane being supplied, rather than combining capacity and speed ranges from unrelated catalogue models.

    Parameter What our technical offer states
    Rated lifting load — t The applicable rating and its load basis, including the grab and other below-hook equipment as required by the selected arrangement.
    Net waste payload — t/cycle Expected waste mass per grab, calculated separately from the total suspended mass.
    Grab volume — m³ Selected volume, geometry, grab self-weight and assumed waste density and filling factor.
    Span, travel and lift — m Runway centre distance, working envelope, pickup depth, hopper discharge height and end approaches.
    Motion speeds — m/min Hoisting, lowering, trolley and bridge speeds, with acceleration and approach settings used in the cycle calculation.
    Handling rate — t/h Calculated performance for the agreed routes, workload split and operating assumptions.
    Duty and environment Mechanism duty, load spectrum, operating hours, enclosure protection and corrosion provisions.
    Controls and interfaces Operating modes, weighing option, alarms, plant signals and any contracted automation functions.
    Building and service interfaces Wheel reactions, rail requirements, electrification, access platforms and grab-service arrangements.

    Check Handling Capacity Before Choosing the Tonnage

    A larger rated load does not necessarily produce more tonnes per hour. The crane must close the grab, hoist, travel, discharge and return; mixing and bunker transfer also consume cycles.

    Illustrative calculation: why feeding capacity can be overstated

    Assume a 5 m³ grab, waste bulk density of 0.35 t/m³ and a filling factor of 0.80. These are example inputs, not specifications of an offered Henan Mine Crane model.

    Calculation Illustrative result
    Waste payload: 5 × 0.35 × 0.80 1.40 t of waste per cycle.
    If grab self-weight is assumed to be 2.00 t 3.40 t total suspended mass before any additional attachments; this is not a selected crane rating.
    A 90-second cycle and 75% productive utilisation 1.40 × (3,600 ÷ 90) × 0.75 = 42 t/h of waste handling.
    A plant feeding 750 t/day evenly over 24 hours 31.25 t/h average furnace feed.
    If mixing and transfer add 50% to feeding tonnage 46.875 t/h total handling demand, before any additional project margin.

    Result: the example arrangement delivers 42 t/h against an assumed demand of about 46.9 t/h. Selecting it solely from furnace feed tonnage would miss the additional workload. We evaluate grab size, route length, cycle time and crane arrangement together to close that gap.

    For the project calculation, measured waste properties and the actual duty split replace these assumptions. The proposal states the performance basis so the acceptance test can use comparable conditions.

    Automation That Matches the Plant’s Operating Routine

    Automation can reduce repetitive operator movements, but the useful specification is the sequence the crane performs and how it handles interruptions. We separate the operating functions in the offer.

    Control level Offered operating scope
    Manual or remote operation Operator-directed picking and discharge, with the contracted motion controls and protections.
    Semi-automatic cycles Operator-selected pickup followed by defined travel or discharge sequences, subject to the agreed interlocks.
    Automatic bunker operation A project-engineered sequence using the contracted position feedback, waste-surface information, hopper signals and zone management. Sensor coverage and recovery procedures form part of the scope.

    Optional functions include weighing, anti-sway, multiple-crane coordination and plant control-system interfaces. The proposal identifies the required hardware and software, the signals exchanged with the plant, and the available operator override and fault-recovery modes.

    Project Reference: Automatic Grab Crane in WTE Service

    Henan Mine Crane’s manufacturer report dated December 2025 records an automatic grab crane entering service at a waste incineration power generation project.

    Published feature Installed project description
    Motion and positioning Variable-frequency control throughout the crane, with absolute-encoder position feedback.
    Handling functions Anti-sway, automatic fixed-point grabbing and constant-weight cyclic operation.
    Operating modes Manual operation, wireless remote control and fixed-point discharge.
    Controls and protection PLC and VFD control, with short-circuit, overload and hoisting-limit protections.
    Future expansion A reserved interface for full automation.

    The report does not publish plant identity, lifting capacity, grab volume or daily throughput. The reserved interface is an upgrade provision; it does not establish fully unattended bunker operation. Equipment for a new project is specified against that plant’s duty.

    Plan for the Day a Crane or Grab Needs Service

    In a waste bunker, a crane can have adequate normal capacity and still leave the plant exposed during maintenance. We develop the service arrangement alongside the operating layout.

    Crane coverage during an outage

    For multiple-crane layouts, we assess whether the available crane can reach the required bunker zones and hoppers. Parking positions and access matter if a stopped crane obstructs a shared runway.

    A workable grab-service area

    We incorporate the agreed grab landing and maintenance position into the layout. A spare grab or replacement wear-part package can be quoted where justified by the maintenance plan.

    Parts and maintenance information

    The supply package can include parts identification, lubrication instructions, inspection guidance and recommended operational spares for the selected drives, brakes, ropes and grab equipment.

    The crane count follows the feeding duty and outage strategy. Two cranes are not automatically full redundancy: the remaining equipment must have both the reach and the capacity required for the agreed reduced or full operating condition.

    Protection for the Waste Bunker Environment

    Moisture, airborne dust and corrosive conditions influence coatings, enclosures, cable systems and machinery access. Our engineering review selects those provisions from the stated service conditions.

    The proposal can identify electrical enclosure protection, cabinet ventilation or cooling, corrosion treatment and service access. Where the plant has a classified hazardous area, equipment suitability and the required certification are addressed for that location. Explosion protection is not assumed from the words “waste crane”.

    Hopper permissives, restricted zones and plant alarm signals can be included in the agreed control interface. Their function and response are documented with the plant team.

    Waste to Energy Crane Price and Quotation Scope

    Waste to energy cranes are quoted by configuration. Span, lifting height, grab type, duty, automation and site-service scope can change the price substantially. A marketplace asking price is useful only when its equipment scope is understood.

    Public seller asking prices checked in 2026

    Public listing Advertised price Scope limitation
    Shandong Intercontinental Huanqiu Heavy Industry Machinery Co., Ltd. — garbage grab crane listing on Made-in-China US$8,800–118,800 per set; reference FOB price. The page presents differing capacity descriptions. This is an advertised configuration range, not a comparable fixed-specification installed WTE system.
    Dafang seller store on DIYTrade — “Garbage grab crane” US$100,000 per piece. The listing does not define a fixed capacity, span or automation package, or establish an installed project cost.

    These are other suppliers’ public asking prices, not Henan Mine Crane quotations or a verified transaction-price range. Freight, duties, building works and site installation are not established by the figures above.

    What your Henan Mine Crane quotation separates

    The commercial offer lists the crane and grab package, controls and automation options, electrification, recommended spares, documentation, packing and delivery basis. Installation guidance, commissioning and training are priced with their stated service scope. Runway steelwork, rails, civil works and plant integration responsibilities are identified so the purchasing team can compare the total project scope.

    Lead time and warranty terms are stated in the offer for the selected configuration and destination.

    From Engineering Drawings to Site Acceptance

    Project stage Deliverables available within the agreed supply
    Engineering review General arrangement, working envelope, wheel reactions, technical schedule and control-interface description.
    Factory acceptance Agreed inspections and tests of crane motions, brakes, limits, control sequences and applicable load-test requirements, with corresponding records.
    Site commissioning Installation checks, travel and hopper-position setup, plant-signal checks and weighing calibration where supplied.
    Operational acceptance A representative waste-handling test using the agreed routes, material conditions and workload split. Factory motion tests alone do not prove site waste throughput.
    Handover Contracted manuals, electrical drawings, parts lists, maintenance information, training and control-system backup or access provisions.

    The acceptance plan ties the performance test to the same assumptions used in crane selection. This gives the plant team a clear basis for checking the supplied equipment.

    Waste to Energy Crane FAQs

    What is the difference between crane lifting capacity and waste payload?

    Waste payload is the waste carried in one grab. Total suspended mass also includes the grab and applicable attachments. Our technical schedule states the rating basis and expected net waste payload separately.

    Can a waste to energy crane run automatically?

    Yes, automatic sequences can be engineered for the agreed bunker layout and plant interfaces. The offered scope identifies sensing, control functions, operator intervention and recovery arrangements; a reserved interface alone does not provide fully unattended operation.

    How many waste cranes does a plant need?

    The number follows the total feeding, mixing and transfer workload and the maintenance strategy. We assess both normal operation and the required operating condition when a crane is unavailable.

    Can you supply a replacement crane for an existing waste bunker?

    We can evaluate a replacement against the existing runway, building clearance, hopper positions and plant interfaces. The proposal includes the crane arrangement and reactions for project coordination.

    Do you provide installation and commissioning support?

    Installation guidance, commissioning assistance and operator training can be included in the offer. The quotation identifies the selected services, site responsibilities and commercial terms.

    What is needed to start a waste crane quotation?

    A bunker layout and short description of daily waste intake, furnace feeding demand and desired operating mode are enough to begin. Henan Mine Crane develops the initial arrangement and identifies the remaining design inputs.

    Henan Mine Crane · Technical information reviewed: 2026

    Get a Waste Crane Arrangement and Itemized Quote

    Send your bunker layout, daily waste intake and preferred operating mode. Henan Mine Crane will develop a proposed crane arrangement, a grab and capacity basis, and an itemized equipment and service quotation.

    Request a Waste Crane Quote
    Email Bunker Drawings

    Email: info@hnksglobal.com
    Henan Mine CraneDiscuss your requirements ↗
  • Waste Handling Crane

    Waste Handling Crane

    Waste Handling Crane

    Henan Mine Crane · Waste-to-Energy Equipment

    Waste Handling Crane

    Engineered grab crane systems for municipal solid waste reception, bunker mixing and incinerator feeding. Select the crane, grab, controls and operating duty as one coordinated plant system.

    Henan Mine Crane supplies project-specific overhead grab crane configurations for waste treatment facilities. Crane capacity, grab volume, throughput, redundancy and automation are established from the waste stream and bunker layout—not from a generic crane tonnage alone.
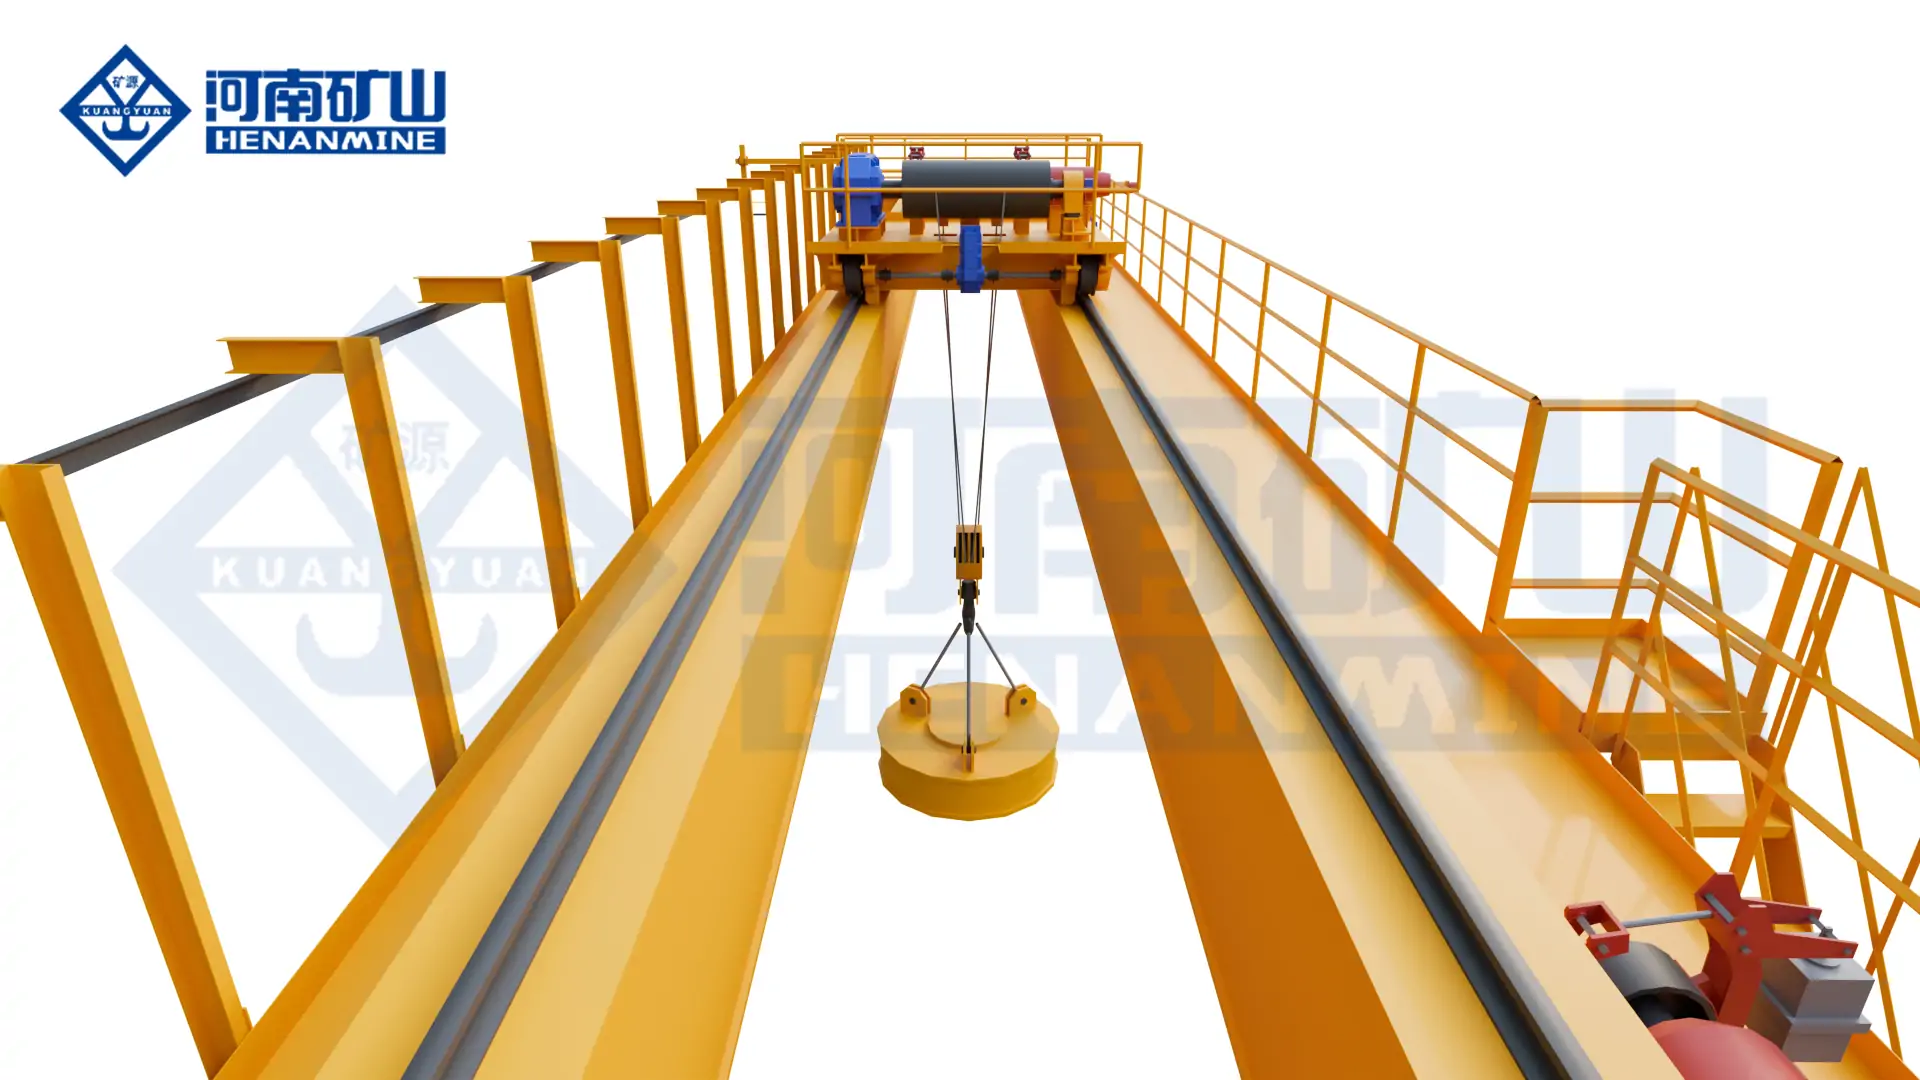
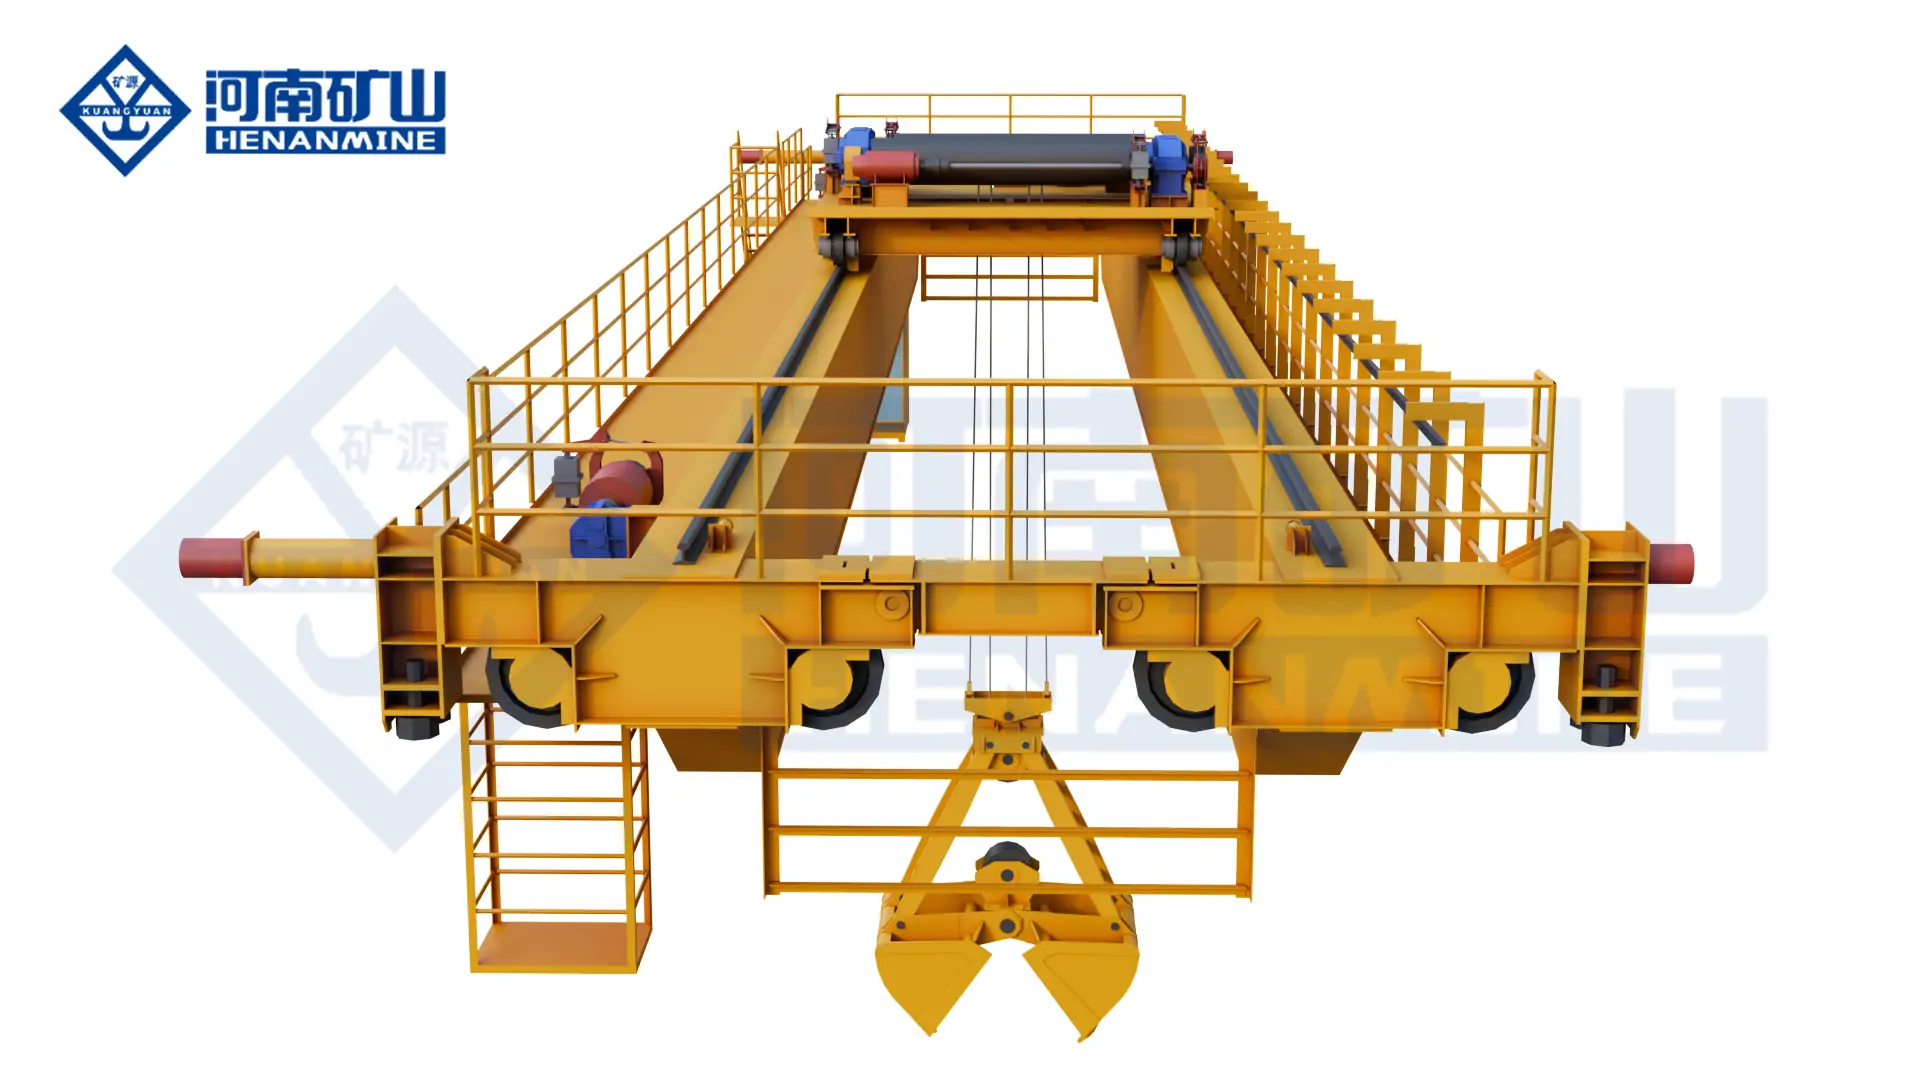
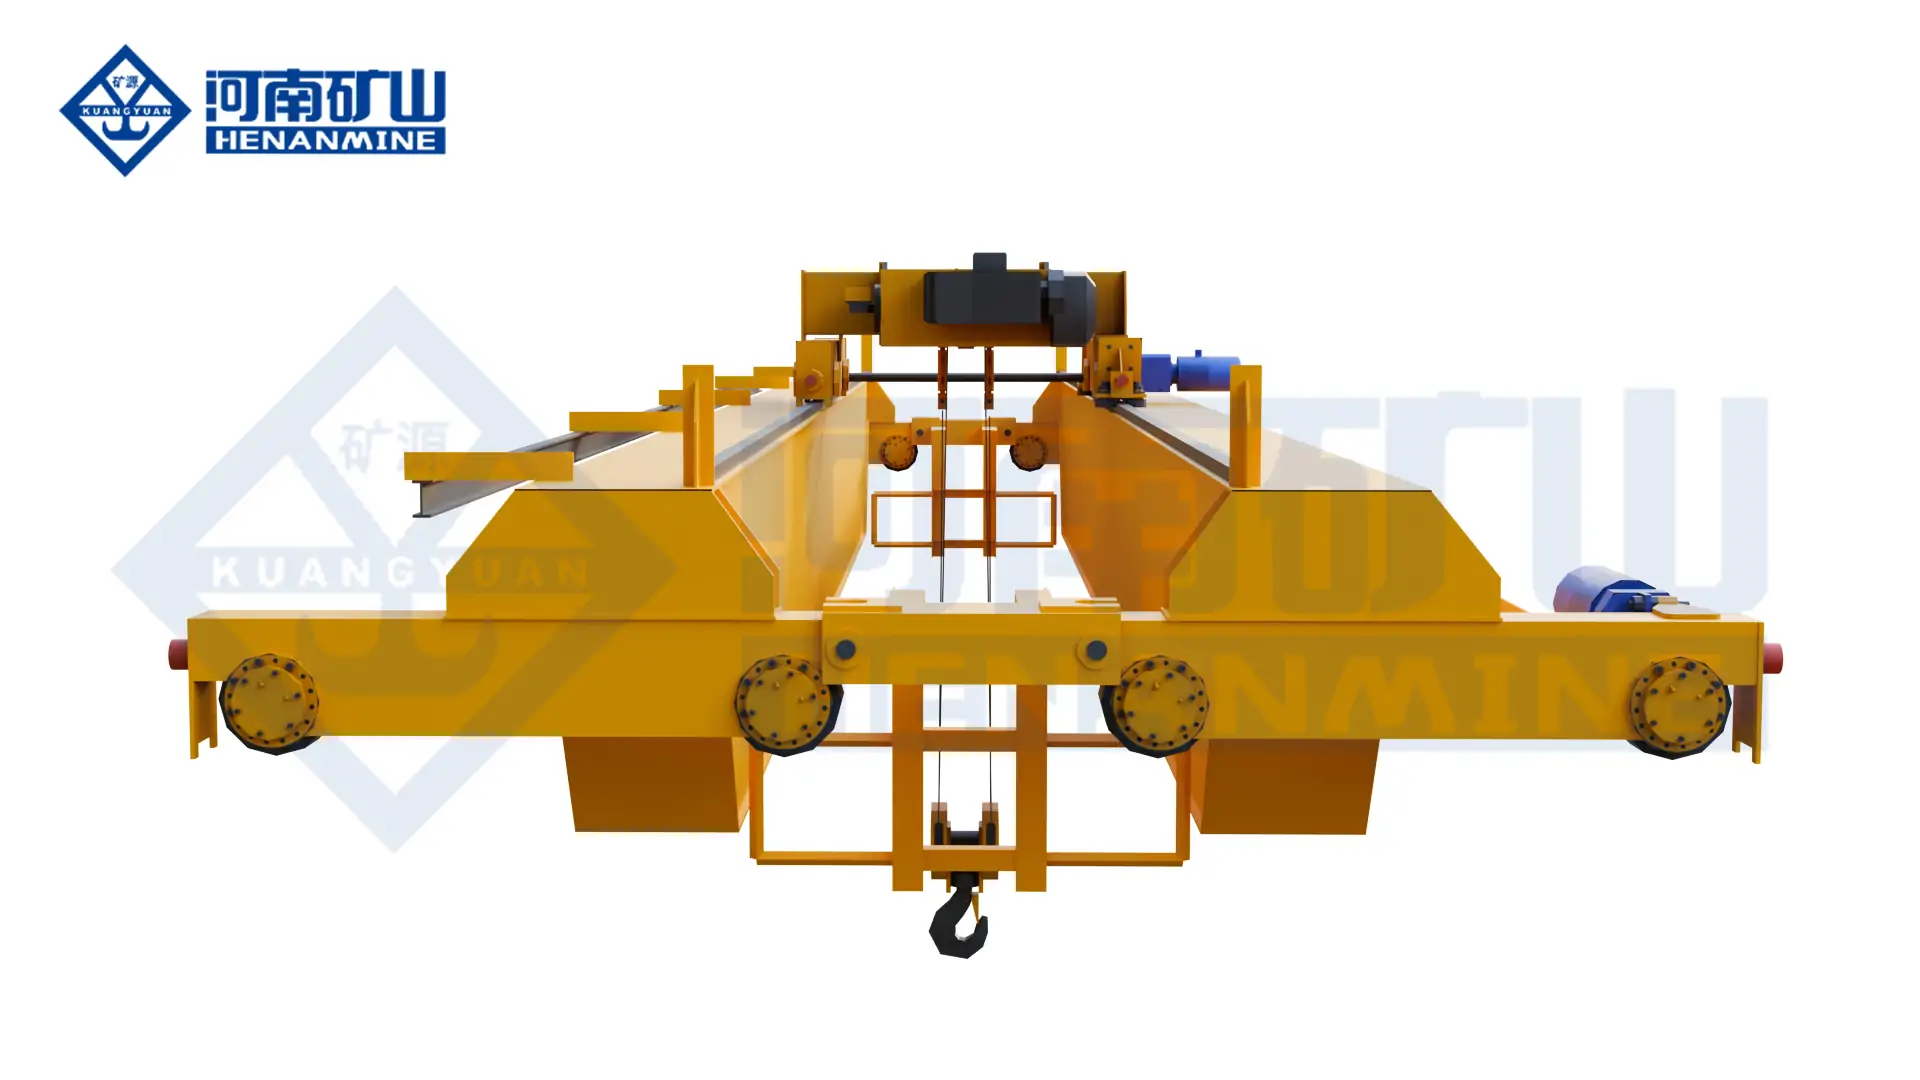
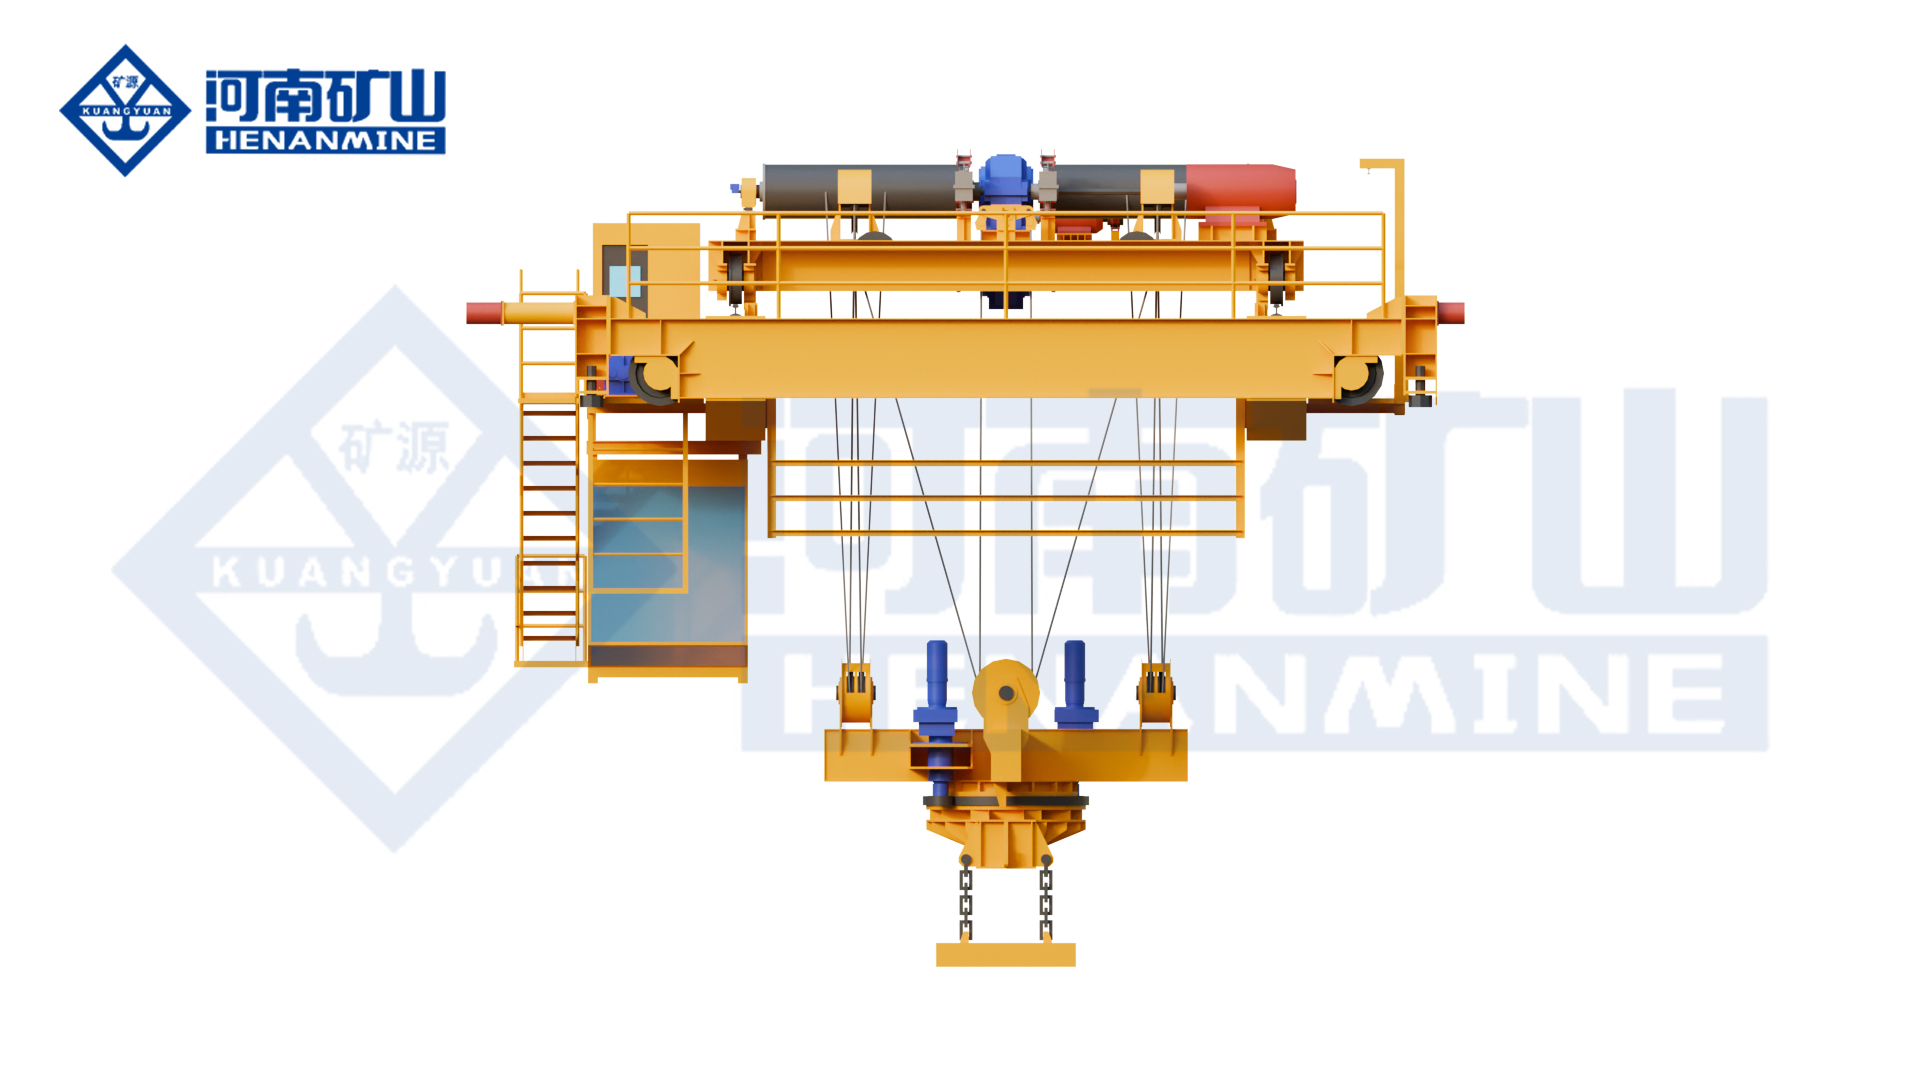
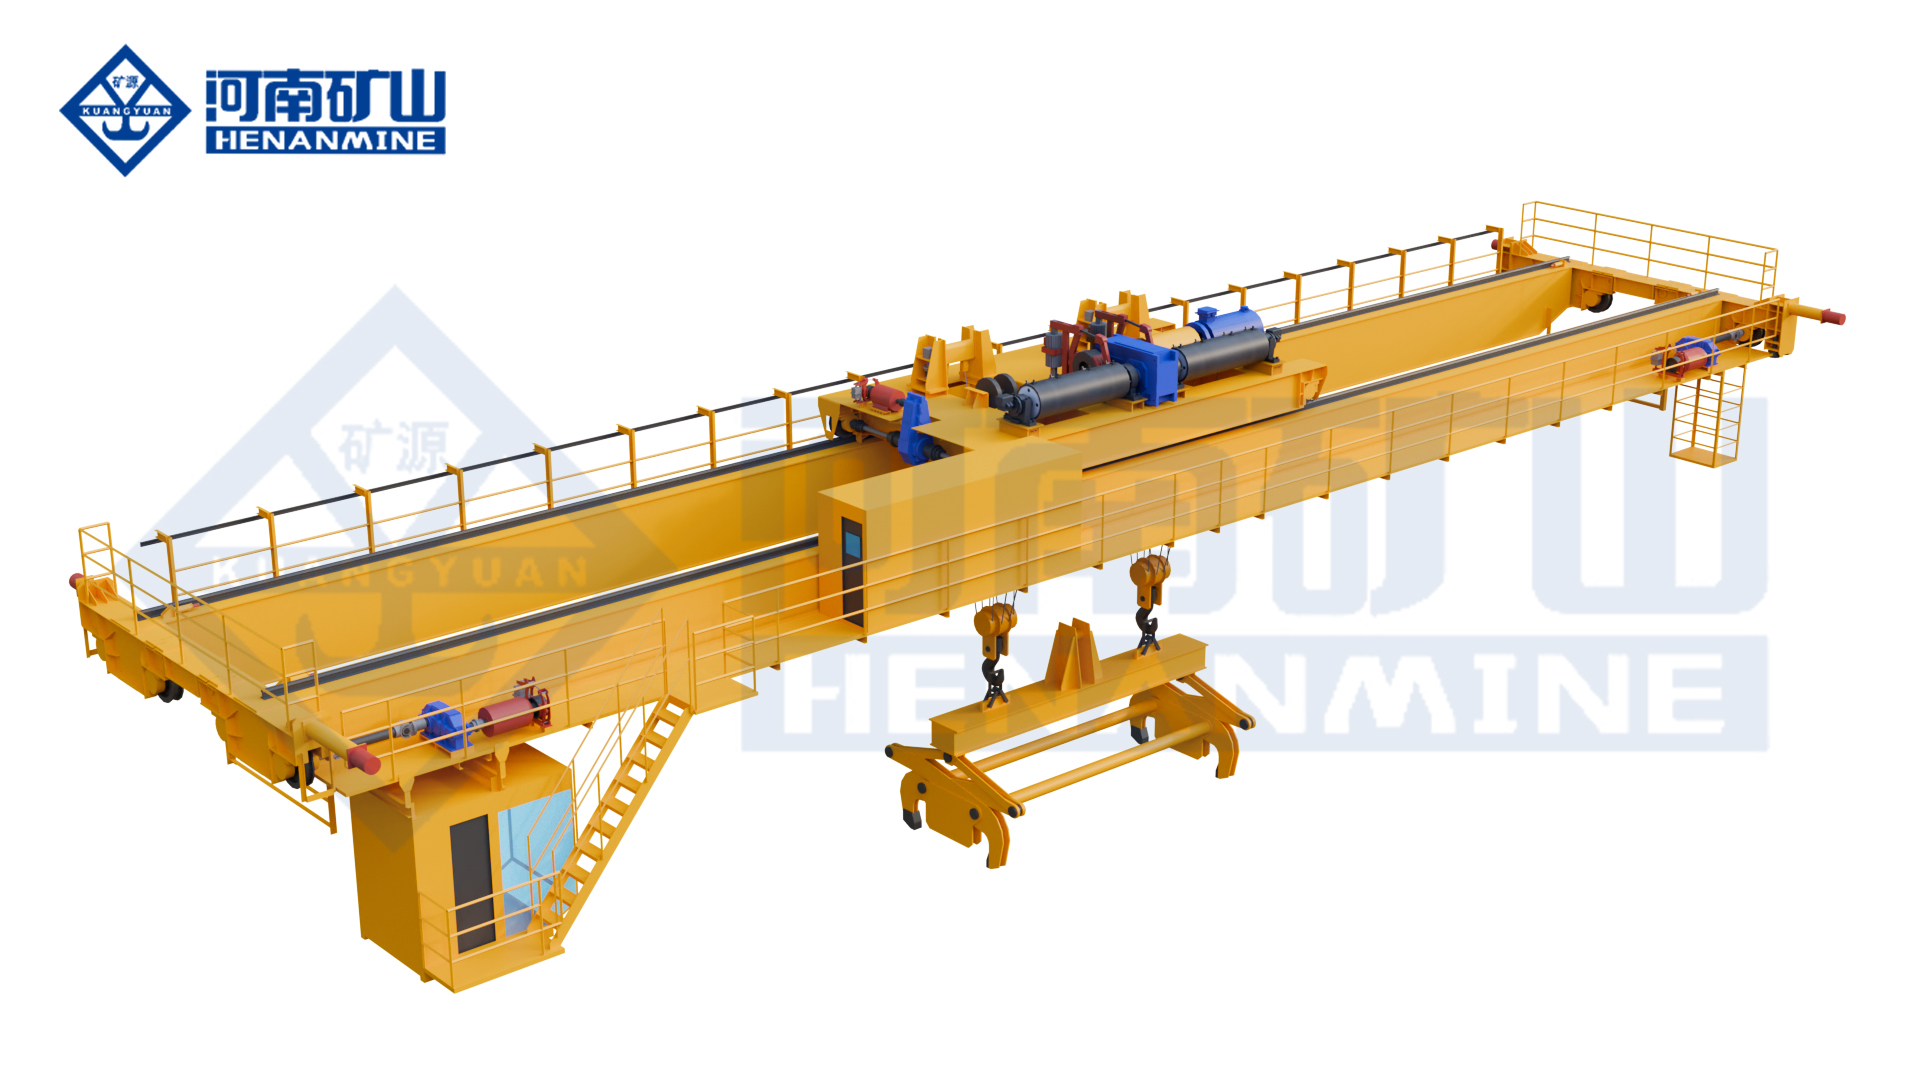
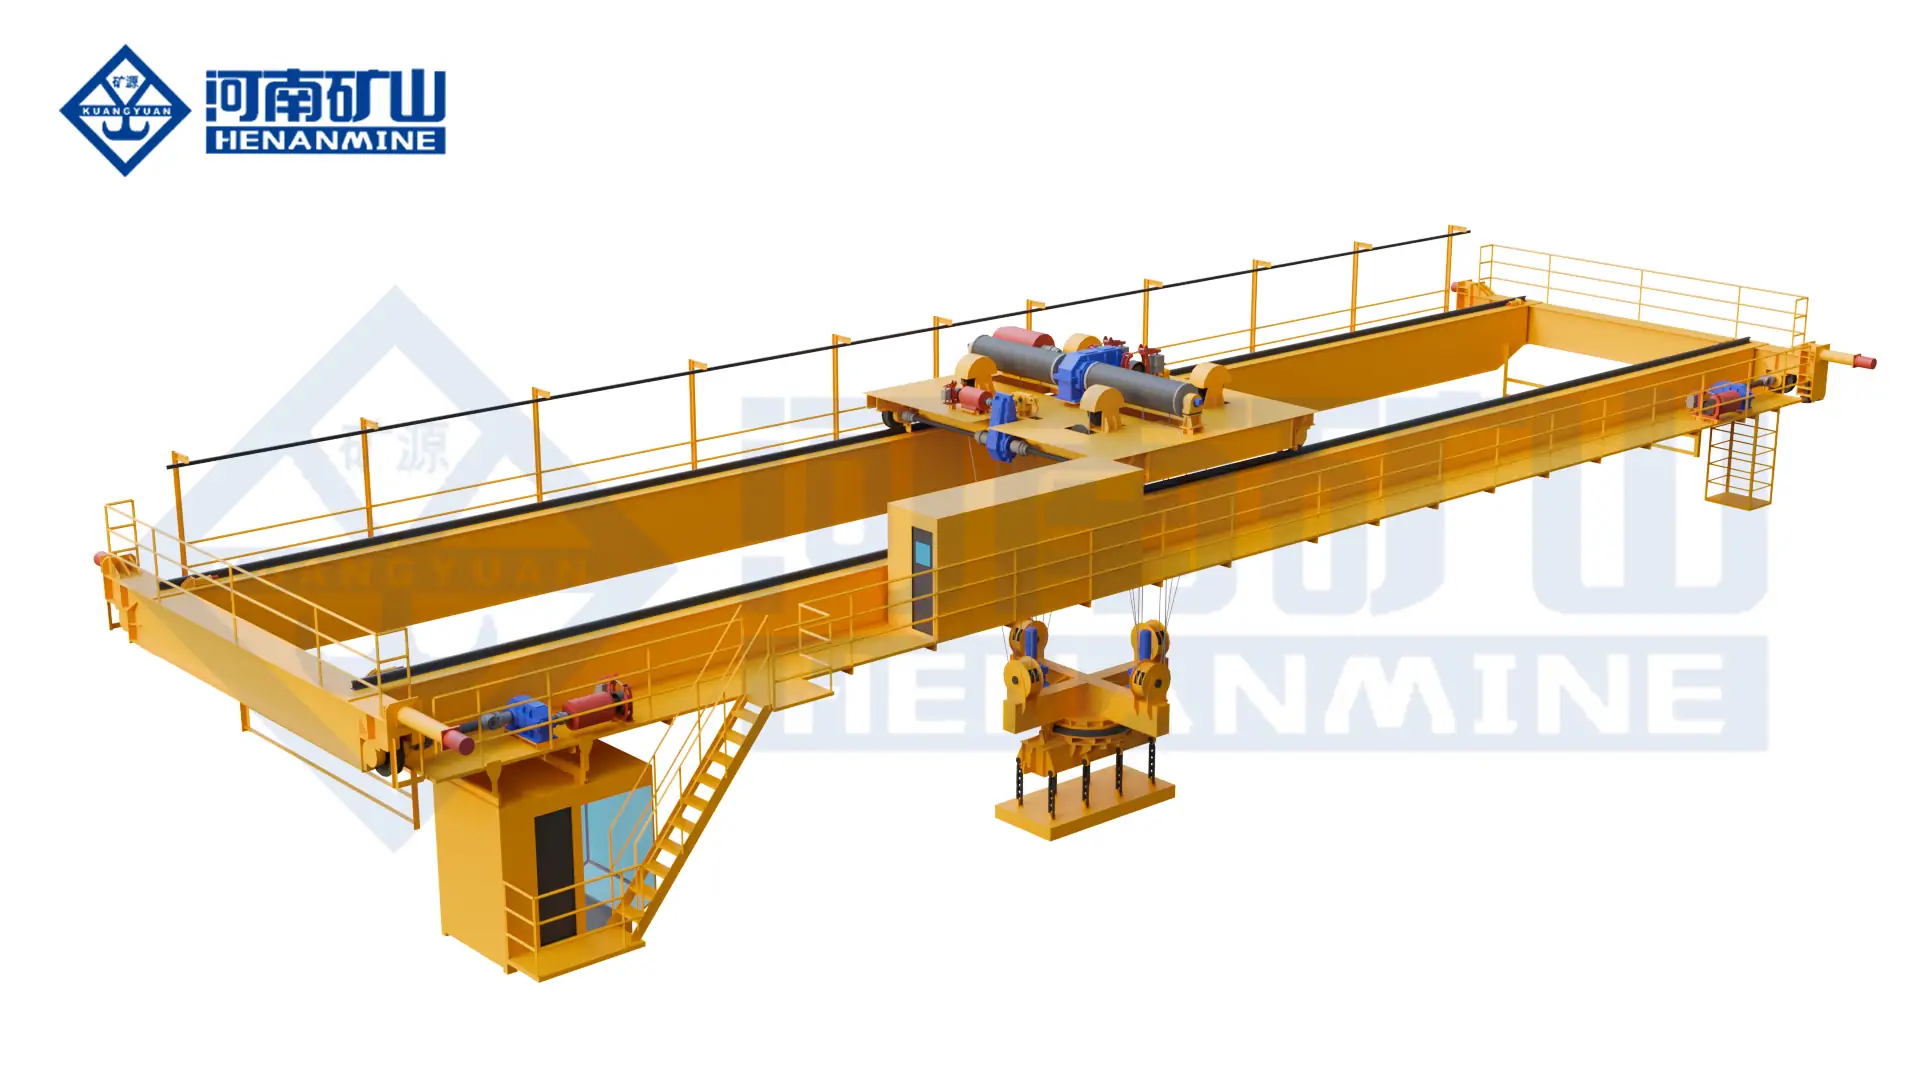
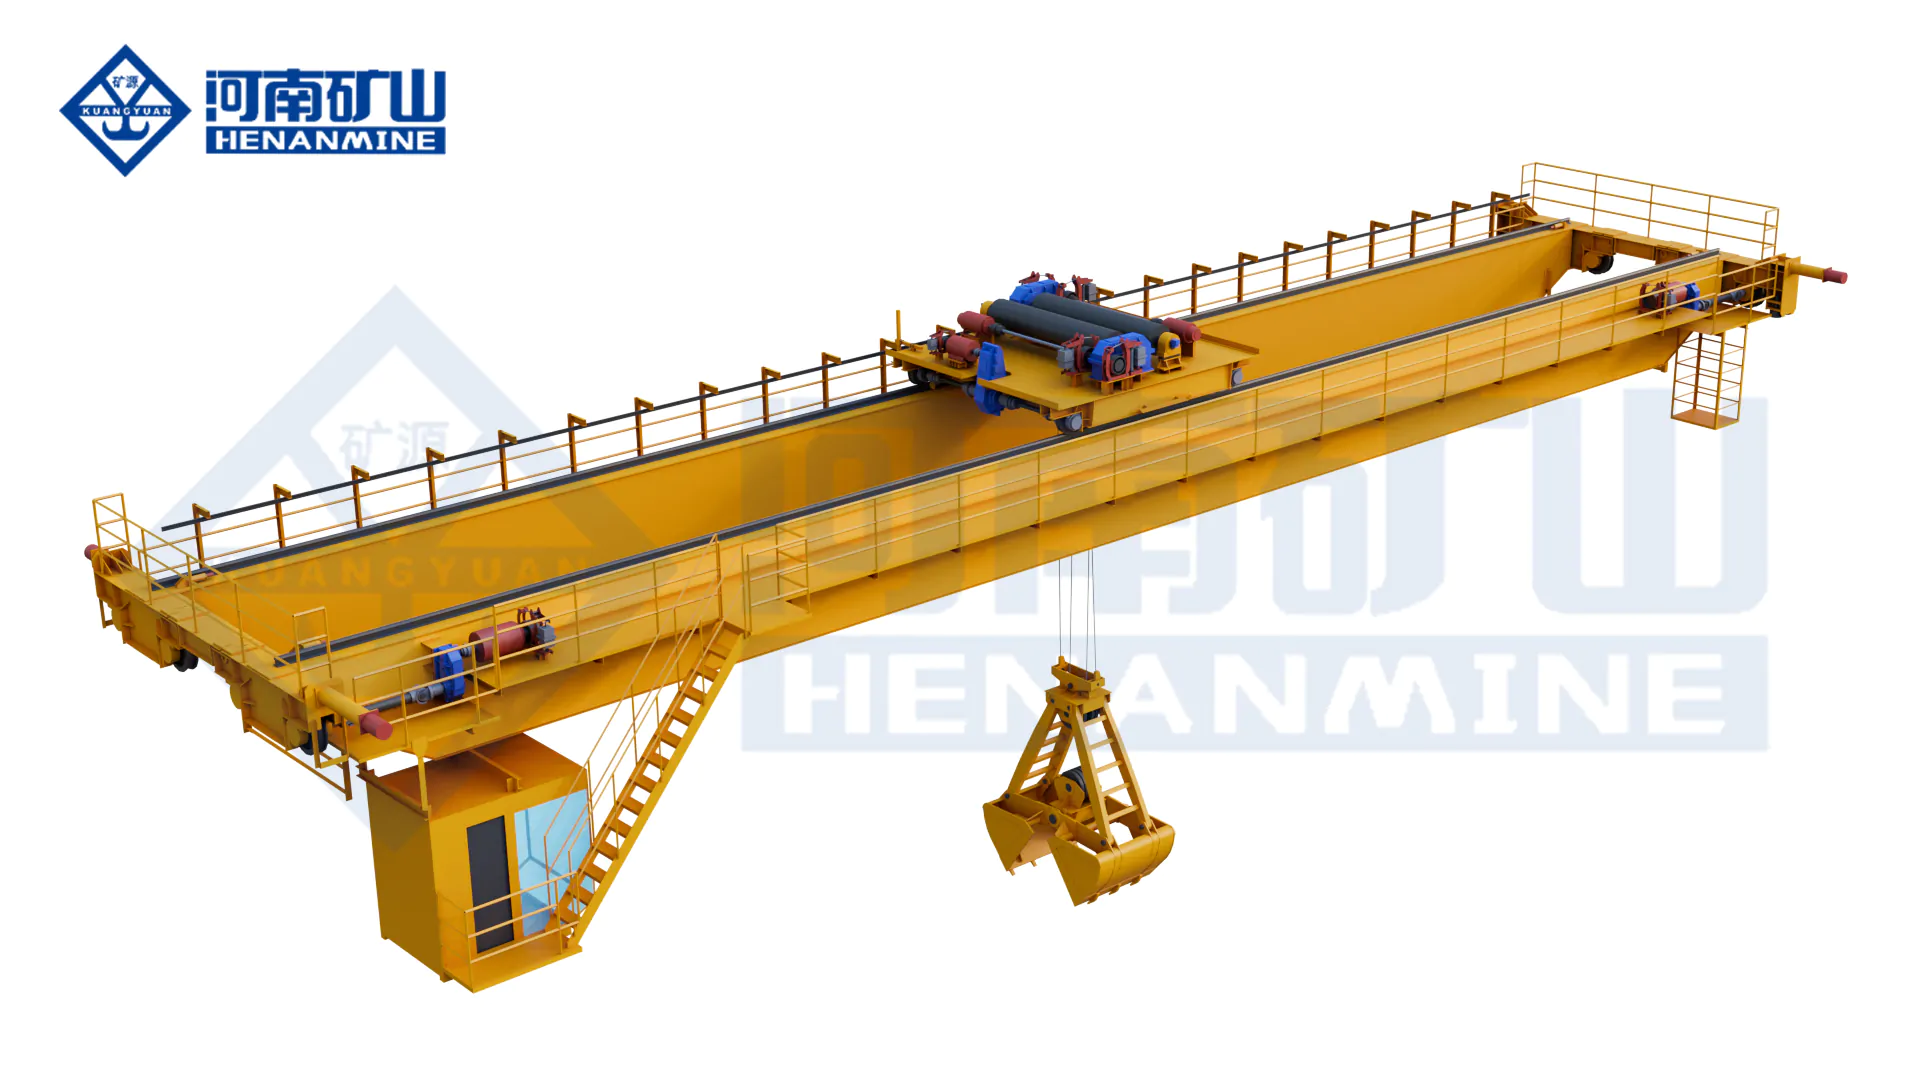
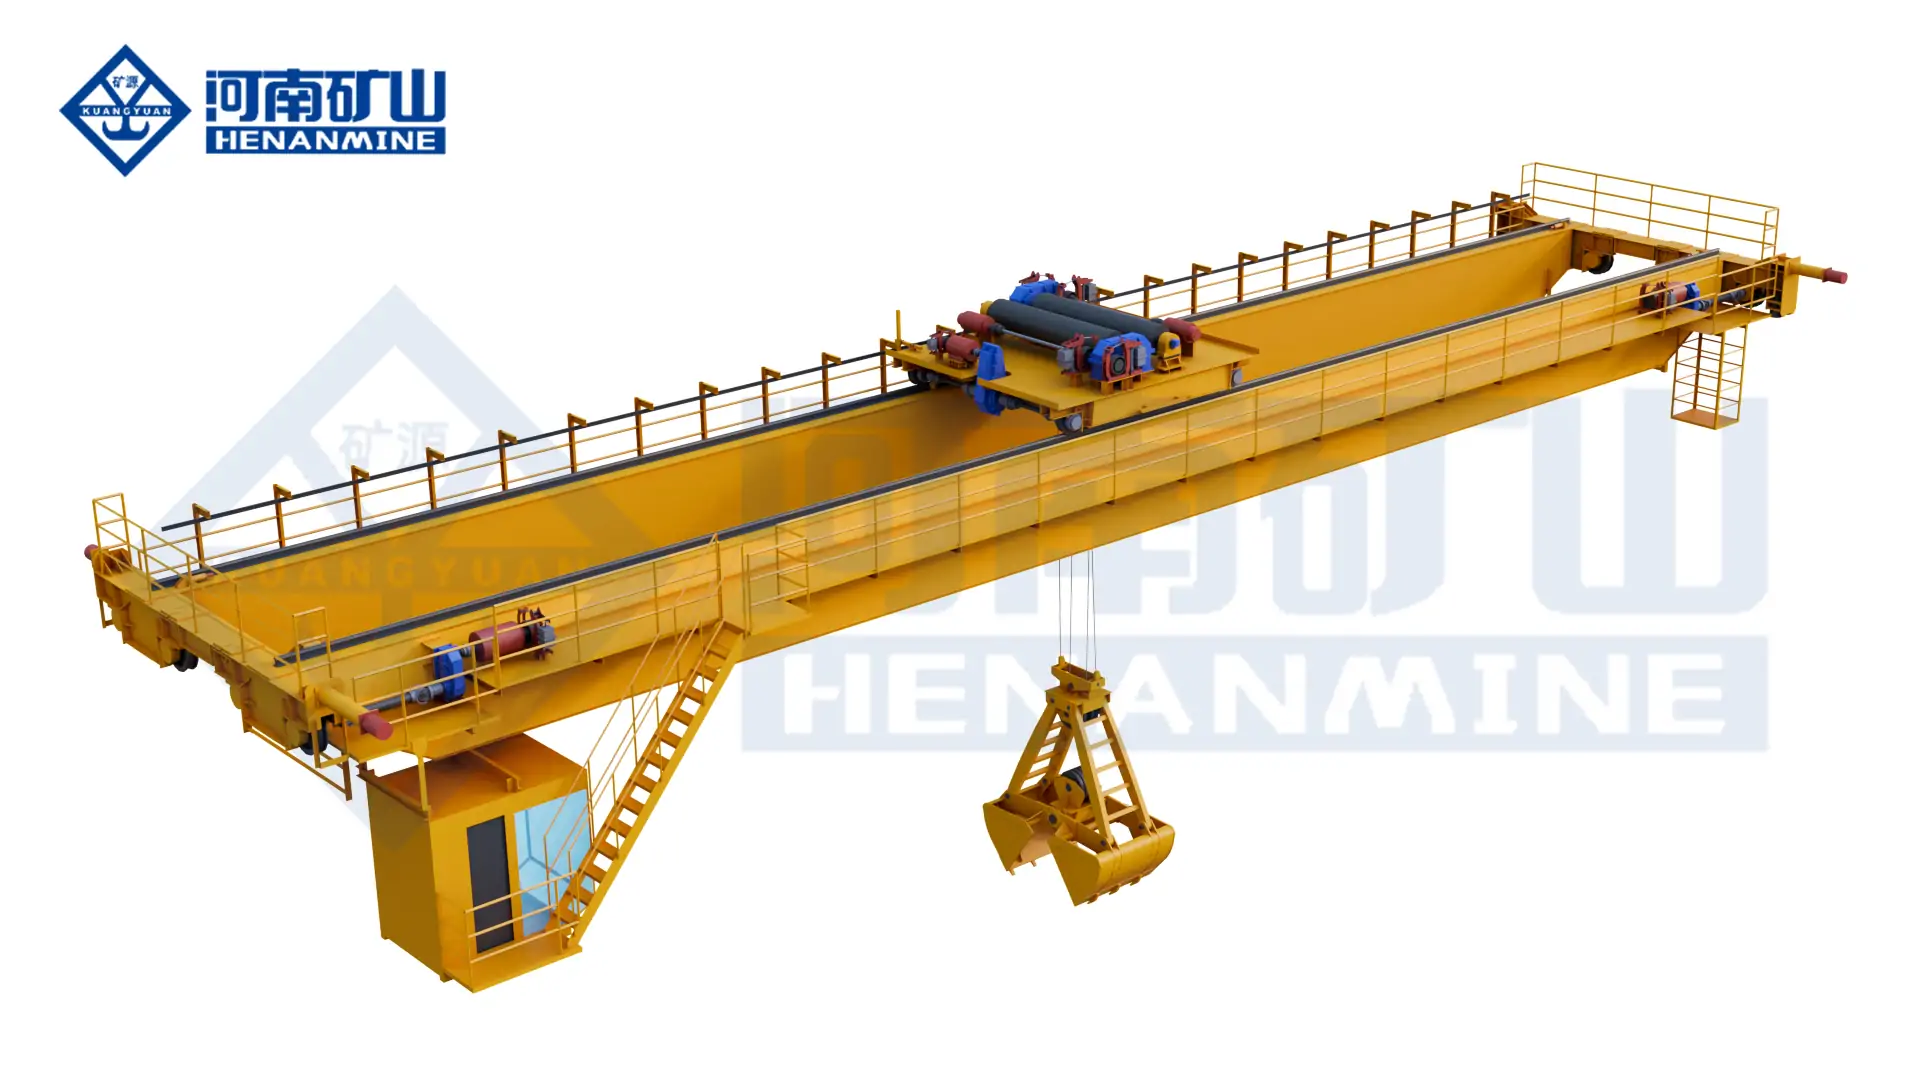
    Henan Mine Crane double-girder grab overhead crane configuration
    Grab crane configuration shown; a waste-bunker crane and bucket are engineered for the actual MSW handling cycle.

    Primary application
    MSW storage pits and waste-to-energy feed hoppers

    Handling functions
    Receiving, mixing, stacking, weighing and feeding

    Control options
    Operator control, assisted cycles or engineered automation

    Commercial scope
    Quoted against plant drawings and operating requirements

    A Crane Designed Around the Waste Bunker

    A waste handling crane works above the storage pit, transfers incoming municipal waste between zones, mixes material to support a consistent feed and delivers defined batches to the incinerator hopper. These operations involve repeated starts, reversals and grab cycles in an atmosphere that can contain moisture, dust and corrosive contaminants. The equipment specification must address both production demand and maintainability.

    The overhead bridge, hoisting mechanism, opening-and-closing system, bucket, runway interface and controls are specified together. A crane selected only by its nominal lifting capacity may not deliver the required tonnes per hour, cover the entire pit or provide the operational reserve needed when one unit is unavailable.

    For recycling or scrap facilities, Henan Mine Crane can assess an alternative grab-and-hook arrangement or a separate material-specific lifting system. A waste-to-energy feed crane is not interchangeable with a ferrous-scrap magnetic crane or an occasional-duty warehouse hoist.

    Choose the Right Waste Handling Configuration

    01 · MSW Bunker Grab Crane

    A double-girder overhead crane with an application-matched grab for wide pit coverage, waste homogenisation and reliable hopper charging.

    02 · Manual or Assisted Control

    Operator-directed pickup and feed, with defined travel limits, speed control, load indication and optional positioning assistance.

    03 · Automated Grab Cycles

    Engineered repeatable pickup, distribution and hopper-feed sequences with approved operating zones and operator intervention provisions.

    04 · Dual-Crane Bunker Coverage

    A duty and standby arrangement where incinerator availability demands an alternative crane during servicing or a unit fault.

    05 · Grab and Weighing System

    A bucket selected for waste density and fill behavior, paired with a weighing arrangement when the process requires batch or feed records.

    06 · Corrosion-Conscious Package

    Coating, sealed electrical equipment and accessible service points specified for the site’s moisture, leachate and cleaning regime.

    07 · Smaller Transfer Station

    A lighter grab-crane option may suit intermittent sorting or transfer work after actual cycle frequency and materials are confirmed.

    08 · Recycling and Scrap Handling

    Grabs or hook-and-grab systems are selected for the actual material; magnetic lifting is considered only for suitable ferrous loads.

    Waste Crane Configuration Comparison

    The selection is based on the operating cycle and the material, not solely on the lowest equipment price.

    Configuration Best-fit operation Design priority Key limitation to assess
    Double-girder MSW grab Frequent bunker mixing and hopper feed Duty, reach, bucket payload and availability Total installed system scope
    Automated MSW grab Defined repeatable feed and distribution cycles Positioning, interlocks and plant integration Commissioning and exception handling
    Single-girder grab Smaller, intermittent transfer duties Building load and cost efficiency May not suit intensive WtE feed duty
    Hook-and-grab Separate approved loose and unit-load tasks Attachment change and load control Not automatically suitable for continuous MSW feed

    Sizing the Grab for Real Waste, Not a Catalogue Number

    Bucket volume is only one input. Actual lifted waste depends on bulk density, grab fill, the moisture and composition of the stream, and the weight of the empty bucket. The crane’s rated load must cover the bucket, its maximum permitted contents and the applicable lifting arrangement. Waste that bridges inside the grab or contains bulky objects may reduce the practical fill and increase cycle time.

    The required hourly handling rate must include incinerator feed and material turning, pit redistribution and time reserved for grab inspection. Travel distances from pickup zones to each feed hopper and permitted motions around pit walls determine a workable cycle. Henan Mine Crane can develop the preliminary grab and drive configuration from a pit plan, waste description, throughput target and operating schedule.

    A nominal 10-tonne crane, for example, does not necessarily lift 10 tonnes of waste per grab: the bucket dead weight is part of the suspended load. The allowable payload must be calculated for the final grab and operating conditions.

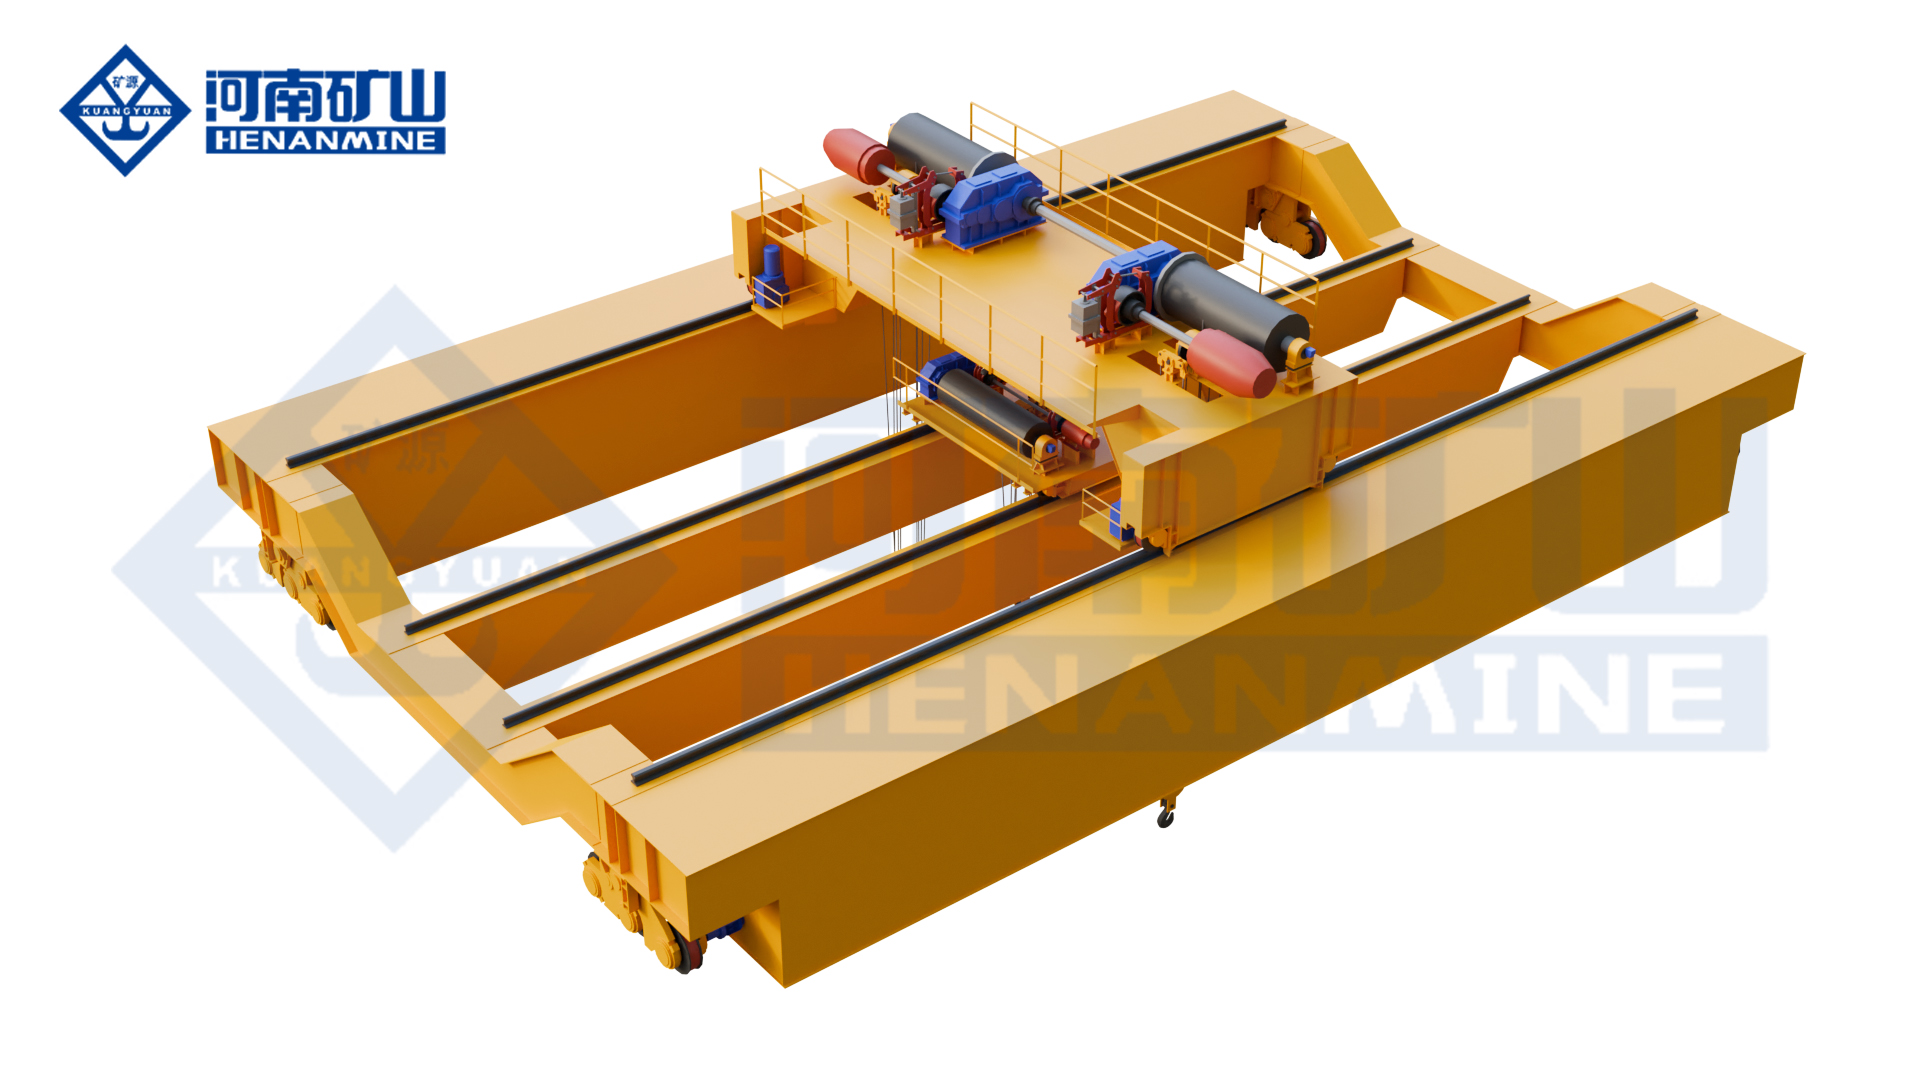
    grab mechanism and bridge crane structure for bulk material handling
    Final grab geometry and rated load are selected for the site’s material and waste-bunker operating envelope.

    Project Specification: Parameters to Confirm

    The following schedule is the basis for an engineered proposal. Values are selected from the facility’s drawings and production demand; no single capacity or span applies to every waste handling crane.

    Parameter Information required for selection
    Waste and process capacity MSW or other material; tonnes per day and required peak feed rate
    Material properties Density range, moisture, bulky items, abrasive content and fill characteristics
    Bucket and crane rating Required grab volume; empty bucket mass plus allowable material payload
    Pit and runway geometry Rail gauge, travel length, rail-top elevation, pit depth and service access
    Hopper arrangement Number and coordinates of receiving hoppers, opening sizes and exclusion zones
    Operating duty Shifts, lifting cycles, load spectrum, permitted downtime and standby policy
    Controls and interfaces Operator station, automation functions, weighing signals and plant control interface
    Site conditions Power supply, ambient conditions, washdown, dust, corrosion and local compliance

    Automation That Fits the Plant’s Operating Plan

    Operator-Directed

    A trained operator supervises pickup, blending and charging. Control stations, sightlines, camera views and override arrangements are established against the bunker layout.

    Assisted Sequences

    Selected travel and discharge moves can be repeatable while the operator retains responsibility for irregular waste, blocked grabs and exceptional loads.

    Integrated Automation

    Defined pickup areas, hopper destinations, weighing, anti-sway functions and operating-state signals can be incorporated after interface and safety review.

    Automatic operation is a specified project function, not an implied feature of every grab crane. The automation proposal should identify its covered zones, interlocks, manual recovery mode, data exchange with the plant and acceptance tests.

    Safety, Availability and Maintenance Access

    Define the Operating Envelope

    End limits, hook/grab travel limits, overload protection, emergency stops and crane-to-crane separation are assessed in the complete layout. Travel restrictions must keep the grab clear of hopper edges, bunker walls and accessible personnel areas.

    Fire detection, waste-bunker ventilation, hazardous-area classification and local electrical requirements are plant-level inputs. Explosion-protected equipment is specified only where the site’s formal classification requires it.

    Plan for Service Continuity

    Where continuous furnace feed is essential, evaluate two-crane coverage, a defined standby sequence and safe access to one crane while the other remains available. The arrangement should be checked against the number of hoppers and feasible service positions.

    Inspection points for ropes, brakes, wheels, bucket pins, hydraulic components where fitted and electrical panels should be reachable without unnecessary exposure above the waste pit. Spare parts and a planned maintenance schedule are included in the operating concept.

    Commissioned Project Example

    Automatic Grab Crane in a Waste-to-Energy Project

    In 2025, Henan Mine Crane placed an automatic grab crane developed for a waste-incineration power-generation project into operation. Its operating functions include automatic fixed-point grabbing and constant-weight repetitive cycles.

    The project crane combines variable-frequency speed control and encoder-based positioning with anti-sway functions. It provides manual, wireless-remote and fixed-point unloading modes and an interface reserved for future automation upgrades. These functions illustrate the available engineering approach; the control scope for each new plant is defined in its project specification.

    For a comparable installation, Henan Mine Crane assesses the purchaser’s bunker geometry, waste stream, required feed rate, operating cycles and plant interfaces before selecting the grab, crane mechanisms and control functions.

    Project Functions

    Application: waste-incineration power generation

    Operation: fixed-point automatic grabbing and repeatable constant-weight cycles

    Motion control: variable-frequency control and position feedback

    Project status: entered operation in 2025

    Waste Handling Crane Price and Quotation Scope

    A waste-bunker crane cannot be priced responsibly from a lifting-capacity figure alone. Advertised grab-crane prices online often concern a basic crane or attachment and do not establish the cost of a waste-to-energy bunker system. An equipment-only price and an installed, automated two-crane plant package are different commercial scopes.

    Henan Mine Crane prepares a project quotation that identifies the priced items, specified functions and exclusions. For procurement comparison, request an itemised offer covering:

    Crane equipment
    Bridge, trolley, hoists, drives, controls and number of units.

    Material handling
    Bucket type, rated volume, spare grab and weighing scope.

    Plant interfaces
    Automation, power feed, runway, structural works and fire-system interfaces.

    Delivery and support
    Testing, shipping terms, installation, commissioning, training and spares.

    Final pricing follows the agreed technical specification and destination. An accurate offer states the quotation currency, trade term, validity period, schedule, warranty scope and responsibility for site installation.

    Prepare a Waste Crane RFQ That Can Be Engineered

    Send the bunker plan with rail elevations, pit dimensions and hopper locations; waste type and daily or hourly throughput; expected grab cycles and operating hours; desired control mode; number of cranes; site electrical supply; destination; and any project specification or applicable local code. An existing plant can also submit crane and runway drawings for retrofit assessment.

    Send Project RequirementsEquipment configuration, technical boundaries and commercial scope can then be assessed together.

    Frequently Asked Questions

    What is a waste handling crane used for?

    In a waste-to-energy plant, it lifts waste from the reception pit, redistributes and mixes it, and feeds the incinerator hopper. The same term can also describe different equipment at recycling or transfer facilities.

    How is the crane’s lifting capacity determined?

    The suspended load includes the empty grab and the maximum approved waste payload. Grab volume, density and filling behavior must be checked together with the selected lifting mechanism and project safety requirements.

    How is the required throughput calculated?

    Assessment considers practical payload per cycle, travel distance, hoisting and grab operation, time spent mixing and feeding, and planned interruptions. Incinerator daily capacity is an input, not a crane cycle specification.

    Is a single-girder crane suitable for an incinerator?

    It may suit a limited or intermittent task, but continuous bunker feeding needs an operating-duty, handling-rate and availability review. A smaller catalogue crane should not be specified as a direct replacement for a high-cycle process crane.

    Does every waste plant require two cranes?

    No fixed number fits every plant. Where furnace feed must remain available during maintenance or a unit fault, dual-crane coverage is commonly evaluated against throughput, hopper positions, operating policy and allowable downtime.

    Can the crane operate automatically?

    Automatic pickup, transfer, weighing and discharge functions can be engineered for defined zones. The proposal must state the supplied functions, safety interlocks, plant communication, exception handling and manual recovery procedure.

    Which bucket is used for municipal waste?

    Grab geometry and actuation are selected for the density, bulky content, abrasiveness, moisture and required volume of the actual waste stream. A bucket intended for coal or ore should not be assumed suitable without evaluation.

    Is an explosion-proof crane required?

    That decision follows the facility’s documented hazardous-area classification and applicable local rules. The waste application alone does not establish a universal explosion-protection rating.

    What affects a waste handling crane’s price?

    Crane rating and duty, span and runway length, grab design, redundancy, controls, environmental protection, test requirements and the delivery and installation scope. A project-specific offer is needed to compare complete systems.

    Can an existing waste bunker be upgraded?

    A retrofit can be considered after reviewing runway condition, wheel loads, rail gauge, available headroom, power supply, hopper geometry and the access needed for installation and future maintenance.

    Related Waste and Bulk-Handling Crane Products

    Intelligent Grab Double-Girder Crane

    A double-girder grab platform for engineered bulk-handling and control configurations.

    Single-Girder Grab Crane

    An option for selected smaller or intermittent bulk-material duties after duty verification.

    Grab-and-Hook Overhead Crane

    Separate hook and grab tasks in approved transfer or recycling operations.

    Double-Girder Bridge Crane

    A bridge-crane structural family for engineered industrial lifting applications.

    Unmanned Grab Crane Application

    Automation concepts for defined bulk-material handling processes and facility interfaces.

    Waste-to-Energy Crane Proposal

    Request a Waste Handling Crane Quote

    Provide your pit and hopper drawings, daily throughput, waste properties, operating schedule, preferred control level and destination. Henan Mine Crane will assess the grab, crane duty, bunker coverage and commercial scope for your facility.

    Henan Mine CraneDiscuss your requirements ↗
  • Warehouse Crane Systems

    Warehouse Crane Systems

    Warehouse Crane Systems

    Henan Mine Crane · Indoor Material Handling

    Warehouse Crane Systems

    Henan Mine Crane supplies warehouse crane systems for the controlled movement of machinery, steel, tooling, long loads and packaged industrial goods between receiving, storage, staging and dispatch areas. Available solutions include top-running bridge cranes, underhung cranes and project-specific indoor lifting systems engineered around the load route, warehouse layout and supporting structure.

    These systems handle suspended industrial loads and are specified independently from automated pallet stacker cranes used within high-bay AS/RS installations.

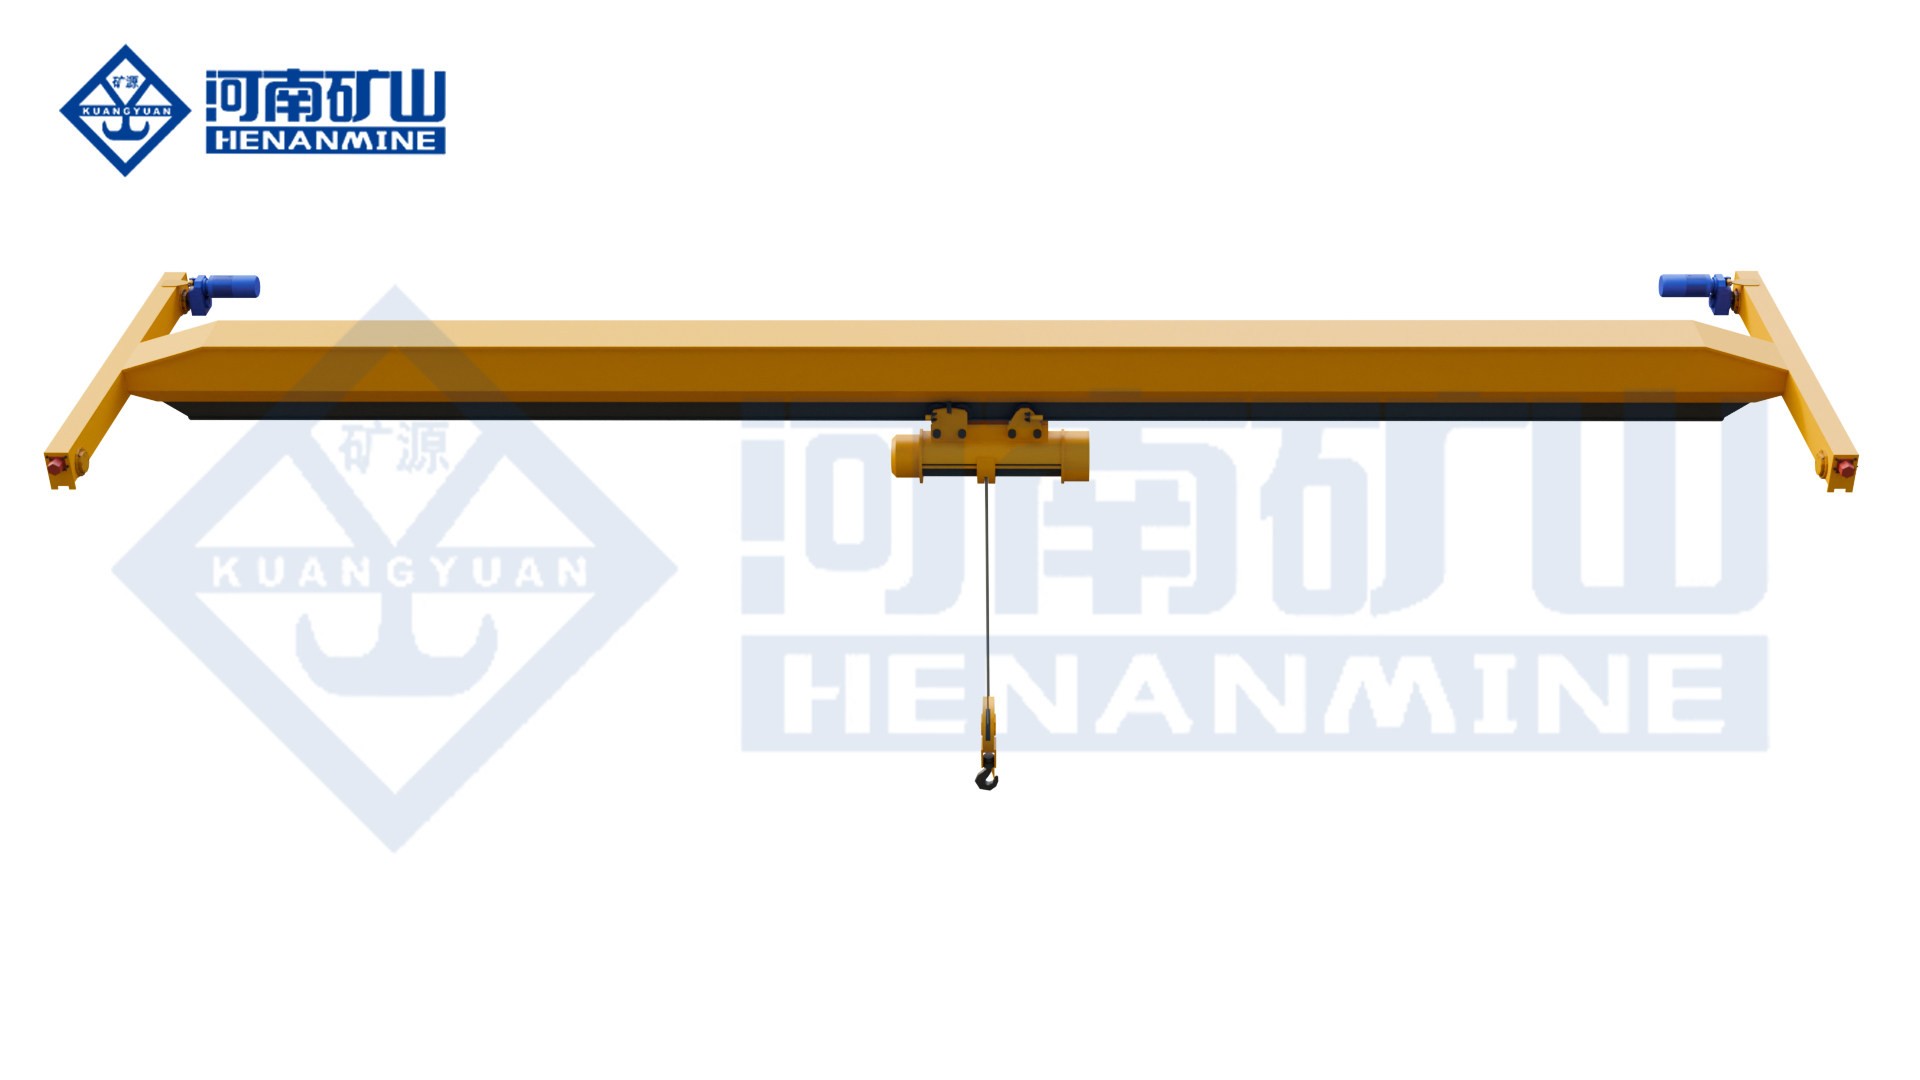
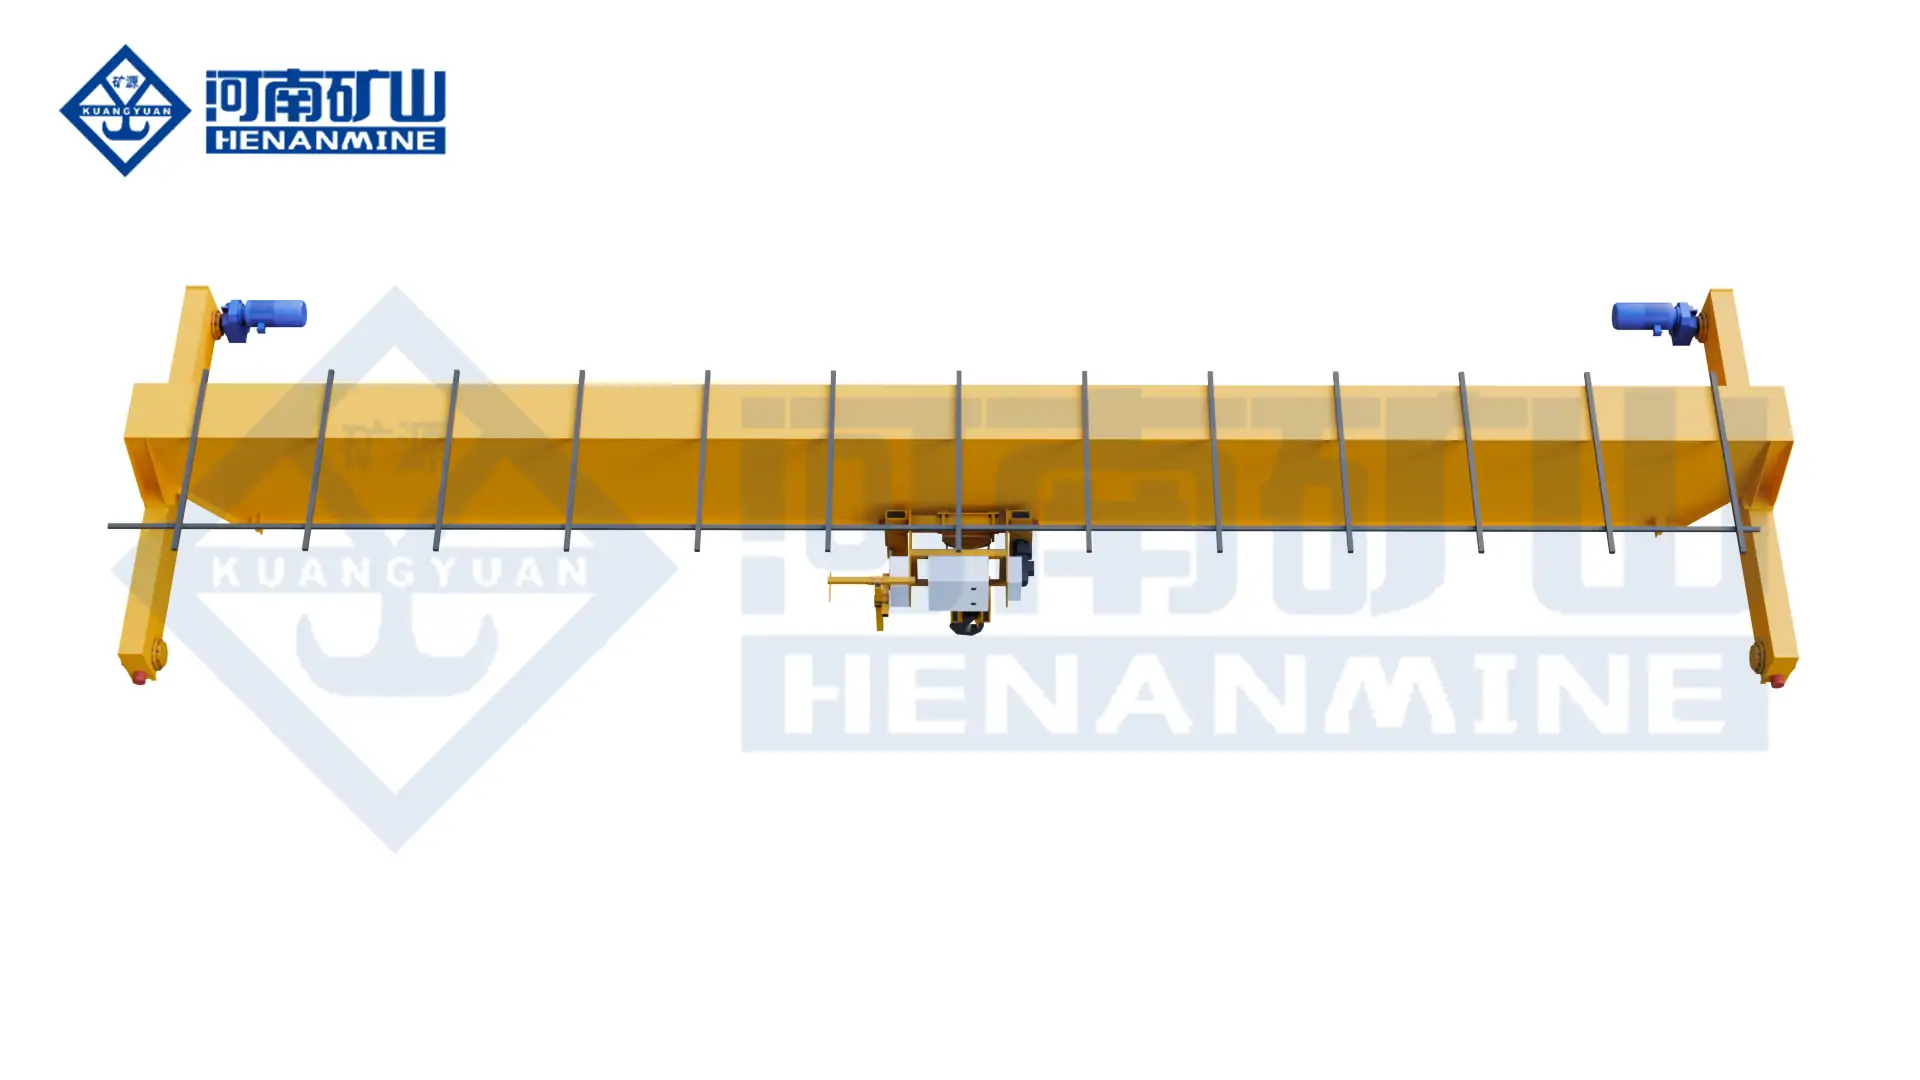
    Single girder warehouse crane for indoor material handling
    Single-girder overhead arrangement for a warehouse bay. Final capacity, span, lift, duty and runway interface are project-specific.

    PRIMARY ARRANGEMENT

    Overhead Bridge Crane

    RUNNING OPTIONS

    Top Running or Underhung

    TYPICAL TASKS

    Storage, Staging and Dispatch

    CONFIGURATION BASIS

    Load, Coverage, Duty and Building

    What Is a Warehouse Crane?

    A warehouse crane is a lifting system selected for material movement inside a storage or distribution building. In industrial warehouses, an overhead bridge crane commonly provides three-axis movement: the hoist raises and lowers the load, the trolley crosses the bridge, and the bridge travels along the warehouse bay.

    The term can also describe underhung cranes, monorails, workstation cranes, jib cranes and floor-running gantry cranes. These systems do not provide identical coverage. The correct choice depends on whether the load must serve a complete rectangular bay, a fixed route, one workstation or several separate handling zones.

    Equipment scope: Henan Mine Crane warehouse solutions are industrial lifting cranes for suspended loads. An AS/RS stacker crane retrieves pallets or totes within storage racks and belongs to a separate warehouse-automation category.

    Warehouse Handling Applications

    Warehouse crane configuration begins with the complete load route. Pickup and placement positions, racks, mezzanines, dock doors, lighting, sprinklers, conveyors and forklift routes establish the required hook envelope and operating clearances.

    Receiving and Unloading

    Warehouse cranes transfer machinery, steel bundles, tooling and other heavy goods from receiving positions to inspection or staging areas. The system layout incorporates vehicle clearance and controlled suspended-load routes.

    Storage and Retrieval

    Industrial loads can be positioned in designated floor or rack locations where forklift handling is unsuitable. The lifting attachment, hook approach and storage access are matched to the handled material.

    Order Staging and Dispatch

    Powered bridge and trolley travel supports the movement of heavy orders between storage, packing, staging and outbound loading positions. Motion speeds and control functions are selected for the required throughput and placement accuracy.

    Equipment Maintenance

    Dedicated lifting coverage supports maintenance of conveyors, compactors, dock equipment and warehouse machinery. Hook approach and lifting height are configured for component removal and replacement.

    Warehouse Crane Specifications

    Each warehouse crane is configured from project-specific load, geometry, duty, building and electrical data. The approved technical schedule and general arrangement drawing define the selected parameters and contractual interfaces.

    Specification Project Information Purchasing Significance
    Rated capacity Maximum payload plus relevant lifting accessories, stated in the required unit Determines the lifting mechanism and structural demand
    Span Runway rail centreline distance or required support geometry Affects girder design, wheel loads, transport and erection
    Lifting height Required lowest-to-highest hook travel and available headroom Defines rope length, hoist arrangement and usable storage height
    Runway length Required bridge travel and end approach at both ends Determines coverage, conductor length and runway scope
    Operating duty Lifts per hour, shifts, travel distances and actual load spectrum Matches motors, brakes, gearing and structure to service
    Motion and control Hoist, trolley and bridge speeds; pendant, radio or specified automation Connects production rate with placement control and operator position
    Warehouse environment Temperature, humidity, dust, corrosion, restricted areas and fire-protection interfaces Defines protection, materials and layout coordination
    Electrical supply Voltage, frequency, phases, earthing and incoming connection point Prevents incompatible equipment and unclear site electrical scope

    Selection Considerations

    01 / LOAD ROUTE

    Warehouse Handling Route

    Receiving, storage, picking, staging and dispatch positions establish the required crane coverage. Aisle crossings and prohibited suspended-load areas form part of the operating layout.

    02 / LOAD

    Load and Lifting Attachment

    Selection data comprise maximum and normal load weights, dimensions, centre of gravity, pickup points and the mass of slings, lifting beams, magnets or grabs.

    03 / BUILDING

    Structural Support and Clearance

    Building plans and sections provide the basis for evaluating runway or roof steel against crane reactions, wheel spacing, hook approaches and maintenance clearances.

    04 / WORK CYCLE

    Operating Duty and Throughput

    Mechanism and structural duty are selected from lifts per hour, operating shifts, travel distances and load spectrum. Repetitive order movement requires a different duty basis from occasional maintenance lifting.

    Warehouse Crane Compared with Other Indoor Handling Configurations

    Alternative configurations are evaluated against the same load route, building drawing and operating cycle. Hook coverage, structural interface, headroom and aisle obstruction are considered together with rated capacity.

    Configuration Coverage Structural Interface Selection Logic
    Top-Running Single Girder Rectangular warehouse bay Runs on supported runway rails Common starting arrangement where capacity, span, duty and headroom permit
    Top-Running Double Girder Rectangular bay with trolley travel across two girders Higher bridge weight and project-specific wheel loads Consider for heavier service, longer spans, trolley arrangements or improved hook height
    Underhung Crane Rectangular bay with potentially close side approach Suspended from verified roof or support structure Useful where floor columns are undesirable and overhead support is suitable
    Monorail or Jib Crane Fixed path or localized circular sector Building-mounted or independently supported Suitable for fixed-route or localized handling where full-bay coverage is unnecessary
    Warehouse Gantry Crane Defined floor route or movable work zone Supported by legs running on floor rails or wheels Consider where an overhead runway is impractical; check aisle and rack interference
    AS/RS Stacker Crane Automated travel inside rack aisles Integrated with racks, controls and warehouse software Different equipment category; not a substitute for an industrial suspended-load crane

    Warehouse Crane System Components

    A complete warehouse crane system integrates the runway and supporting structure, crane bridge, hoisting mechanism, electrification, controls and safety interfaces. Commercial proposals should define the supply boundary for each system component.

    01

    Runway and Supports

    Rails, beams, columns or suspended supports

    02

    Bridge and End Trucks

    Girder, wheels, drives, buffers and stops

    03

    Hoist and Trolley

    Rope, drum, hook, brakes and trolley motion

    04

    Power and Controls

    Panels, conductors, festoon, pendant or radio

    05

    Safety and Interfaces

    Limits, warnings, clearances and warehouse traffic

    Warehouse Layout, Headroom and Hook Coverage

    Warehouse span alone does not establish usable hook coverage. The general arrangement defines side approach, end approach, highest hook position and the lowest hook level required to clear racks, equipment and vehicles.

    The crane envelope is coordinated with pallet racking, mezzanines, lighting, sprinklers, ventilation, cable trays, dock doors and roof bracing. Shared forklift and pedestrian areas require designated transfer zones and prohibited suspended-load routes.

    • Dimensioned warehouse plan and building cross-section
    • Rack elevations, aisle widths and fixed obstructions
    • Pickup and placement heights throughout the handling route
    • Maintenance access around the hoist, trolley and travel drives
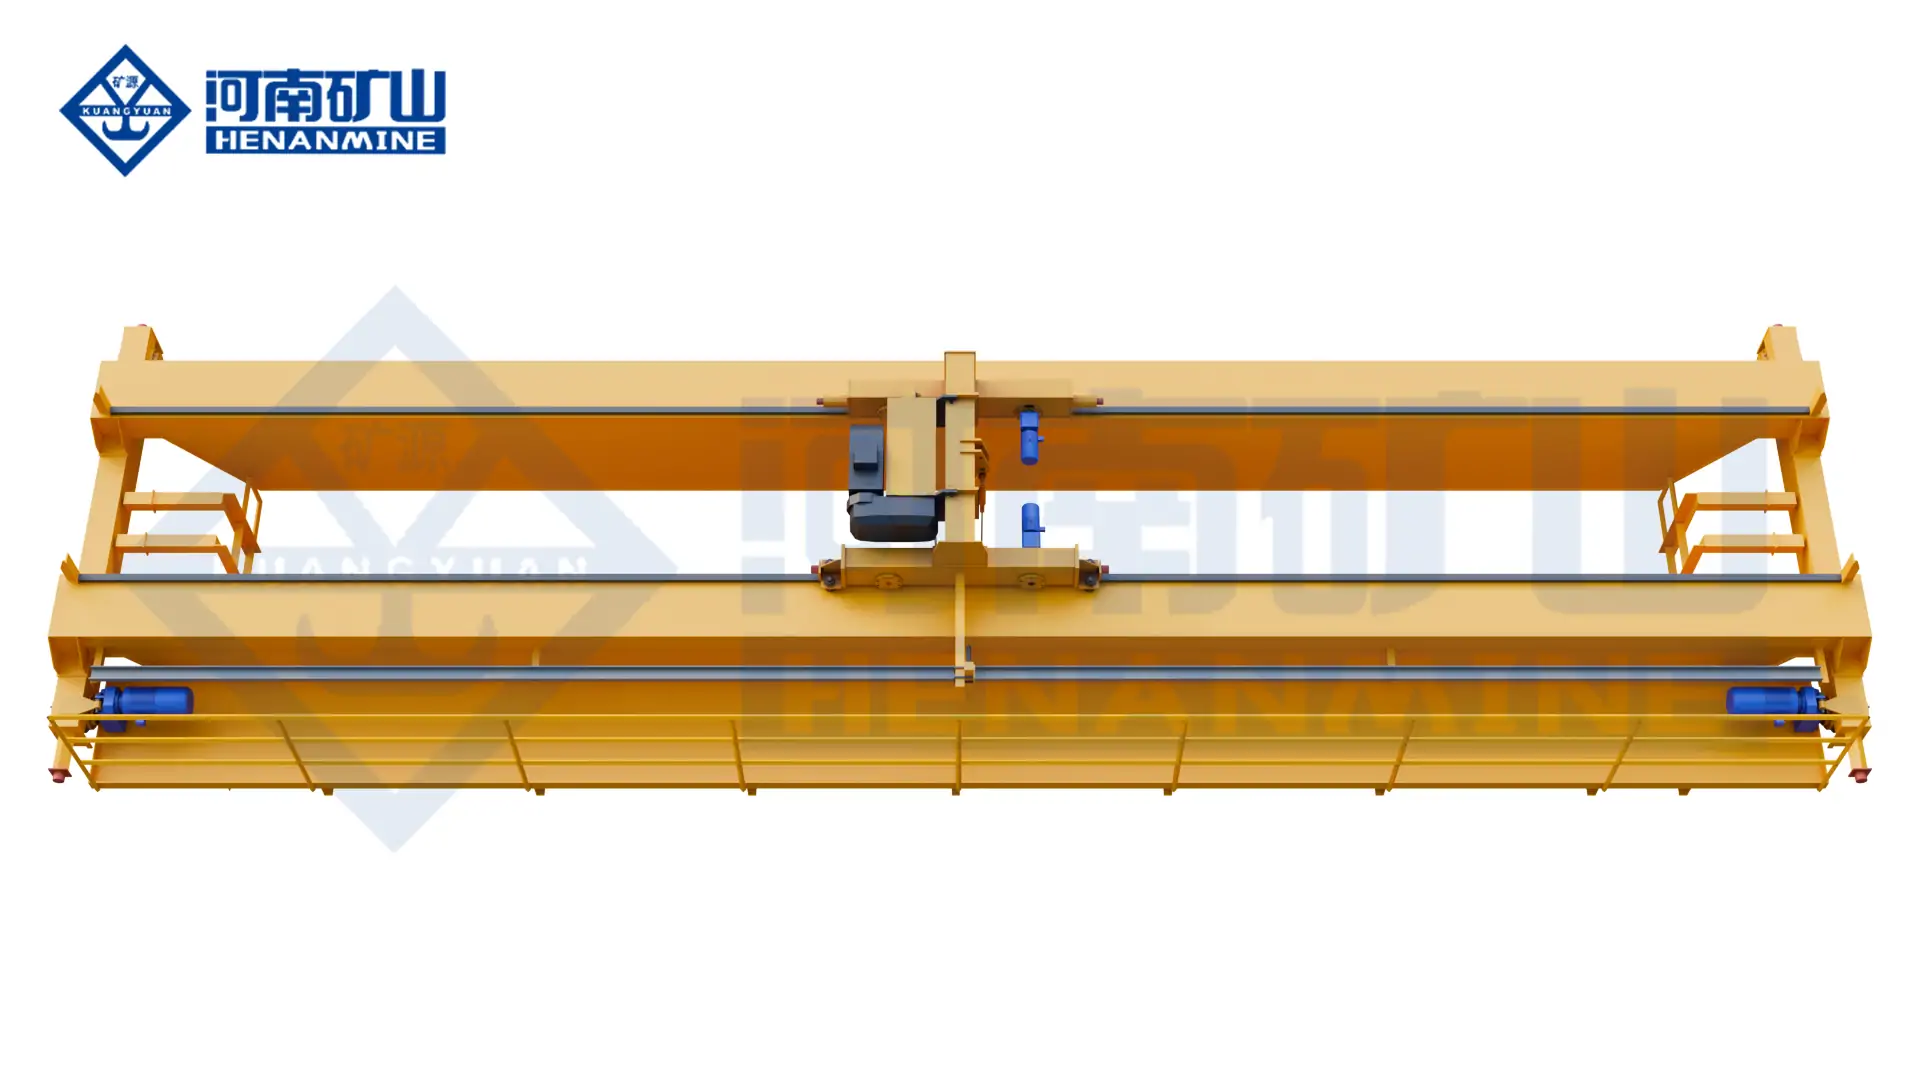
    Double girder warehouse bridge crane showing indoor hook coverage
    Double-girder arrangements may support different trolley, duty and hook-height requirements; suitability depends on the project.

    Load Handling, Hoist and Operating Duty

    The heaviest item establishes only part of the requirement. A warehouse that repeatedly stages heavy orders may need a different hoist, brakes, travel mechanisms and control response from a crane used occasionally for maintenance.

    Load Definition

    Rated-capacity evaluation includes the payload and the mass of lifting beams, slings or other below-the-hook attachments, together with load dimensions and centre-of-gravity variation.

    Motion Selection

    Hoisting, trolley and bridge speeds are selected from travel distance, throughput and positioning requirements. Variable-frequency control provides smoother acceleration, deceleration and load placement where specified.

    Attachment Interface

    Hooks, spreader beams, magnets and grabs serve different materials. The technical schedule defines attachment power, storage position, dead weight and the resulting usable hook height.

    Duty Classification

    Crane and mechanism duty are derived from operating cycles, load spectrum, travel distances and service conditions. The quotation states the applicable classification and design basis.

    Runway, Building and Warehouse Integration

    Suspended warehouse crane and overhead runway arrangement
    A suspended arrangement depends on verified support points, runway geometry and building capacity.

    Structural coordination requires crane wheel loads, wheel spacing, horizontal forces, support details and installation tolerances. Existing runways are evaluated from their structural condition and the reactions generated by the proposed crane, not from nameplate capacity alone.

    New-build projects benefit from crane integration before finalization of roof steel, columns, racks and building services. Retrofit projects require surveys of runway condition, rail alignment, clearances and incoming electrical supply before approval of the crane arrangement.

    • Runway scope, rail profile, end stops and conductor system
    • Responsibility for structural verification and required modifications
    • Assembly space, unloading route and erection access
    • Interfaces with racks, services and fire-protection equipment

    Warehouse Crane Safety and Control Configuration

    Safety functions and operating controls are configured for the destination requirements, crane arrangement and warehouse traffic pattern. The commercial proposal defines crane-mounted equipment, site interfaces and operating responsibilities.

    Load and Motion Protection

    The selected protection package can include overload protection, motion limits, service and holding brakes, emergency stopping and travel warnings.

    Operator Position

    Pendant, radio remote or cabin control is selected according to visibility, travel distance, operating exposure and site procedures.

    Shared Warehouse Space

    Pedestrian routes, forklift traffic, racks, doors and transfer zones form part of the operational risk assessment. Multiple-crane installations can incorporate anti-collision functions or defined operating restrictions.

    Inspection and Access

    The system layout provides safe inspection and maintenance access. Contract documentation defines testing records, manuals, labels and site-acceptance requirements.

    Applicable crane, electrical, inspection and workplace requirements are defined according to the destination country and contract. The technical proposal states the agreed design basis, duty classification, documentation scope and acceptance requirements.

    Warehouse Crane Price

    Warehouse crane pricing is established from the lifting capacity, span, lifting height, operating duty, crane configuration, controls, warehouse interfaces and contractual supply scope. A technically valid commercial offer therefore requires the warehouse drawing and defined operating conditions.

    Cost Component Principal Price Drivers Commercial Definition
    Crane Equipment Capacity, span, lifting height, single- or double-girder structure, hoist or trolley design and operating duty Bridge, end carriages, hoisting mechanism, travel drives, controls and specified protection
    Runway and Supports Runway length, rail profile, supporting beams or columns, structural modifications and installation tolerances Supply responsibility and civil or structural interfaces are stated separately
    Electrical and Control System Power supply, conductor length, control method, variable-frequency drives, anti-collision and automation functions Incoming-power boundary, mobile electrification and site connection responsibilities are defined
    Delivery and Site Services Packing, destination, freight, unloading, erection access, commissioning, testing and training Incoterm, exclusions, local works and acceptance responsibilities form part of the commercial schedule

    Comparable quotation basis: Commercial evaluation should use an identical technical specification and itemized inclusion schedule covering crane equipment, runway, electrification, freight, unloading, erection, commissioning, testing, training, duties and taxes. The Overhead Crane Price page provides a complete cost-component overview.

    Manufacturing and Project Documentation

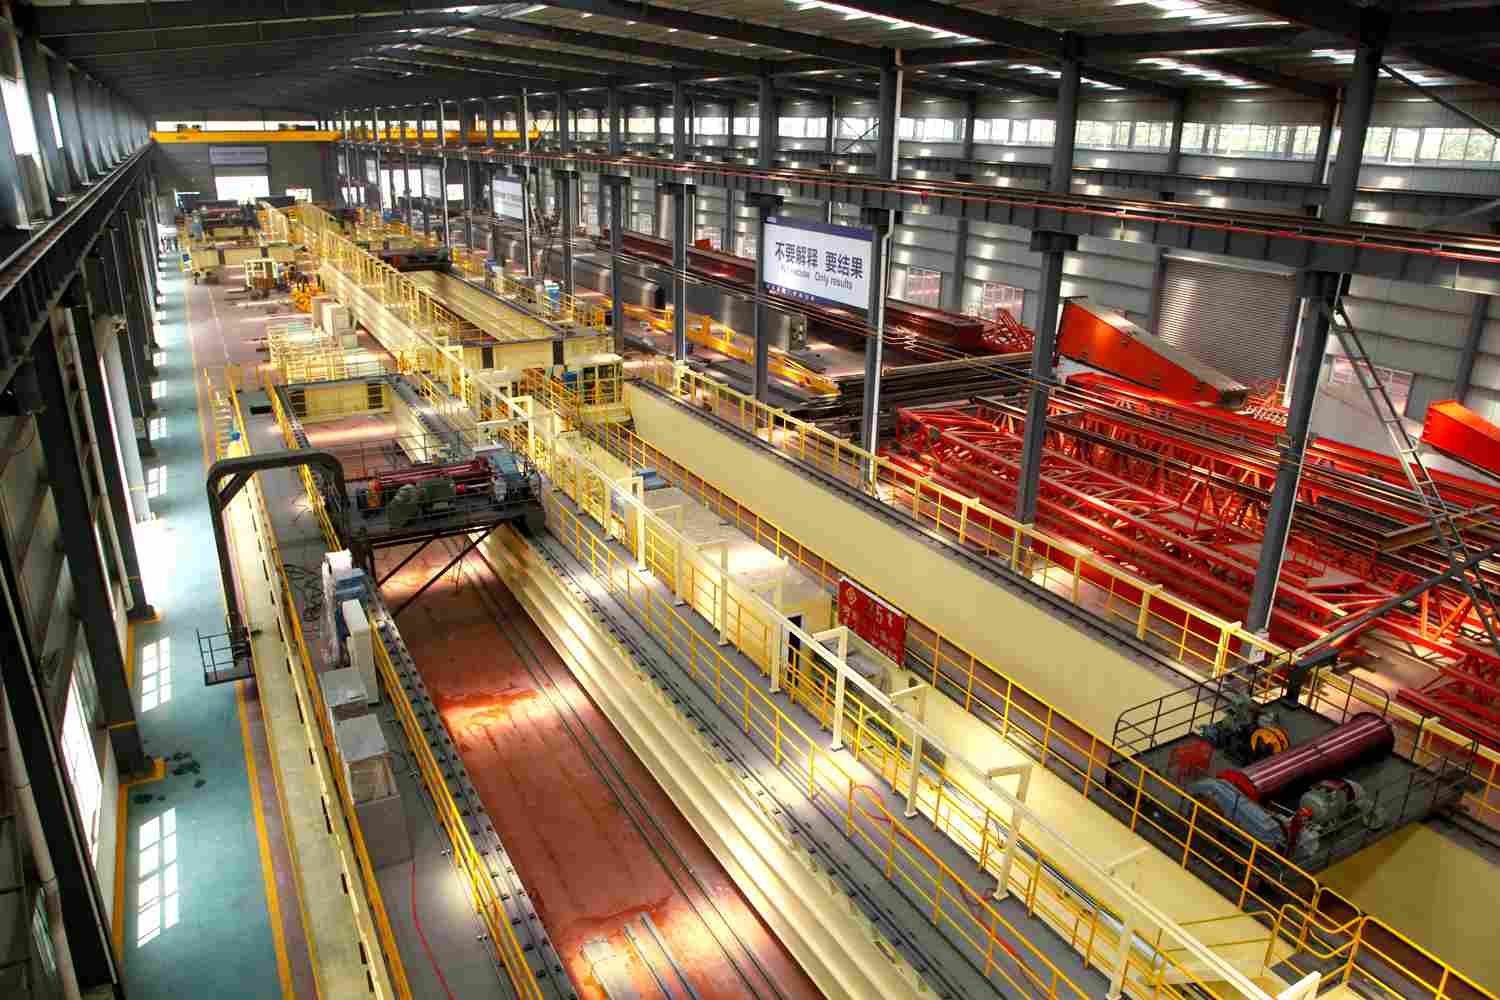
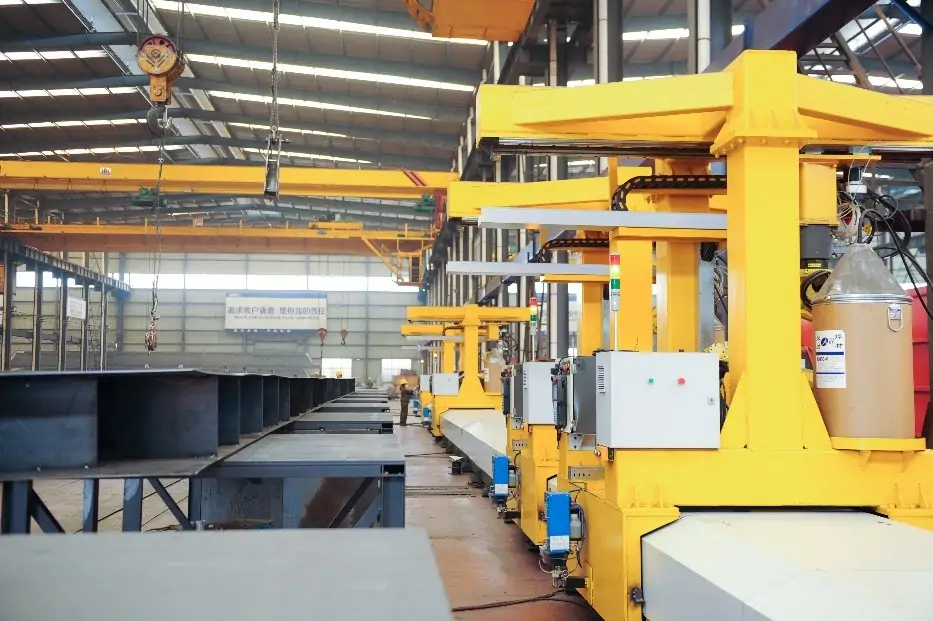
    Henan Mine Crane manufacturing workshop for warehouse crane production
    Structural fabrication and crane assembly at a Henan Mine Crane manufacturing facility.

    Henan Mine Crane manufactures crane structures and integrates the hoisting, travel, control and electrical systems in accordance with the approved project specification. The agreed documentation package establishes the equipment configuration and warehouse interfaces. Henan Mine Crane Manufacturing Facilities.

    • Approved general arrangement drawing and warehouse-interface schedule
    • Component specifications and controlled substitution procedure
    • Inspection stages, factory-test scope and acceptance records
    • Operating manuals, electrical drawings and spare-parts documentation
    • Specified standards, conformity documentation and language requirements

    Installation, Commissioning and Maintenance

    Site Preparation

    Site readiness includes completed and surveyed runways, an available assembly area, protected nearby inventory, incoming power and suitable access for unloading and erection equipment.

    Erection and Commissioning

    The commissioning plan defines mechanical and electrical inspections, functional testing, applicable load testing, documentation handover and operator familiarization.

    Lifecycle Maintenance

    Inspection and maintenance intervals are established from the operating duty, environment, supplied manuals and local requirements. Coverage includes the hoist, brakes, ropes, wheels, rails, electrification and controls.

    The warehouse operator remains responsible for site procedures, trained personnel, inspections and safe use under applicable requirements. The contract should define where the equipment supplier’s scope ends and local responsibilities begin.

    Warehouse Crane FAQ

    What type of crane is used in a warehouse?

    Industrial warehouses commonly use overhead bridge cranes for full-bay coverage. Underhung cranes, monorails, jibs, workstation cranes and gantry cranes serve different structural or localized handling needs.

    Is a warehouse crane the same as a warehouse stacker crane?

    No. A bridge crane lifts suspended industrial loads across a bay. An AS/RS stacker crane travels inside storage aisles to place and retrieve pallets or totes as part of an automated warehousing system.

    Which configuration is appropriate: single-girder or double-girder?

    Single-girder cranes are commonly selected where capacity, span, duty and headroom permit. Double-girder configurations can support heavier service, longer spans, alternative trolley arrangements or different hook-height requirements. Final selection is based on the complete warehouse and operating data.

    Can a crane be installed in an existing warehouse?

    Installation is feasible subject to a site survey and engineering verification of the building, runway, clearances, electrical supply and erection access. Existing steelwork may require reinforcement, modification or an independent support system.

    Can a warehouse crane operate above pallet racks?

    Warehouse cranes can serve suitable rack or floor positions where the hook, attachment and load retain a clear operating path. Rack height, aisle width, sprinklers, lighting and restricted travel zones form part of the layout assessment.

    How much does a warehouse crane cost?

    Pricing is determined by capacity, span, lifting height, duty class, crane configuration, control system and supply boundary. Runways, supporting steel, freight, installation and local electrical work may be quoted separately. A project-specific price is prepared from the warehouse drawing and operating specification.

    Does the price include runway beams and installation?

    Inclusion depends on the agreed commercial scope. The quotation schedule identifies responsibility for crane equipment, runway rails or beams, supports, electrification, transport, unloading, erection, commissioning and testing.

    Can radio remote control be supplied?

    Pendant and radio remote controls are available according to operator position, visibility, travel distance and site practice. The proposal defines the primary control method and any required backup arrangement.

    What information is required for a warehouse crane quotation?

    Quotation data comprise rated capacity, load and attachment details, span, travel length, lifting height, operating duty, warehouse plan and section, existing structure, environmental conditions, electrical supply, destination and required delivery or installation scope.

    Request a Warehouse Crane Quote

    Henan Mine Crane prepares project-specific warehouse crane proposals from the lifting requirement, building geometry, handling route and commercial supply scope. Complete project data support accurate configuration, interface definition and quotation.

    • Maximum load, normal loads, dimensions and lifting attachment
    • Span, travel length, lifting height and rack or building clearances
    • Lifts per hour, shifts, travel distances and control preference
    • Power supply, environment, destination and delivery or installation scope
    Henan Mine CraneDiscuss your requirements ↗
  • Thermal Power Plant Crane Systems

    Thermal Power Plant Crane Systems

    Thermal Power Plant Crane Systems

    Henan Mine Crane · Turbine Hall, Coal Handling and Maintenance

    Thermal Power Plant Crane Systems

    Overhead and gantry crane systems for turbine-generator installation, planned overhaul, coal handling and power plant equipment maintenance.

    A thermal power plant crane must match the lifting task in its specific plant area. Turbine-hall cranes are selected from heavy erection and overhaul loads, hook coverage and runway capacity. Coal-handling cranes are selected from grab payload, material properties and operating cycles.

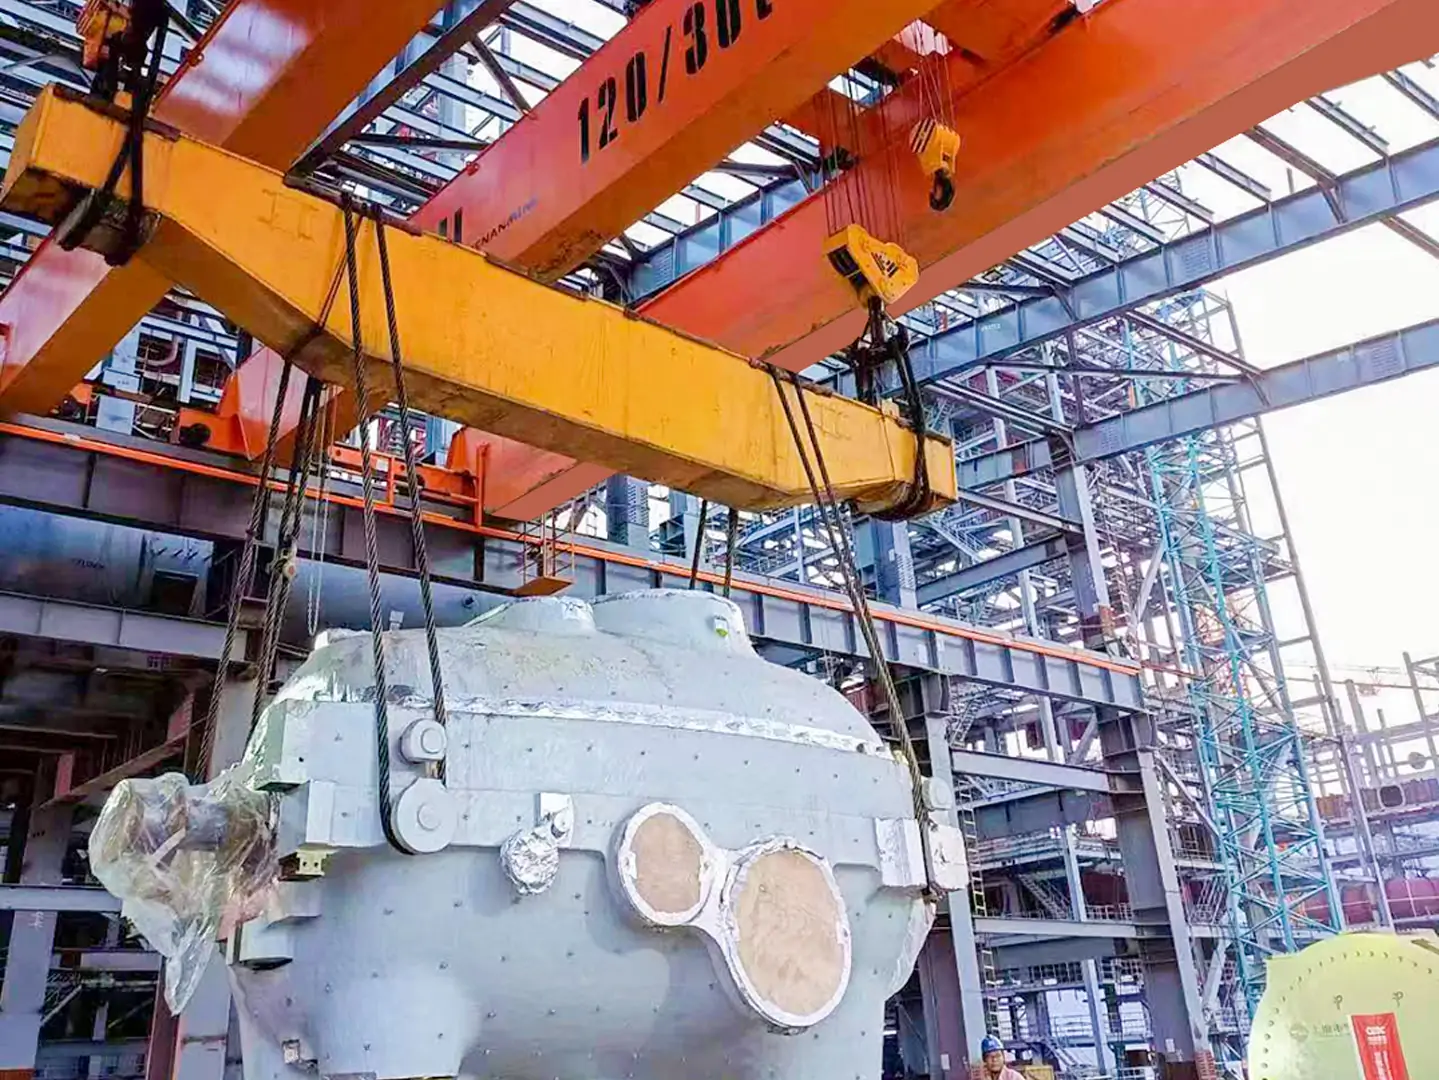
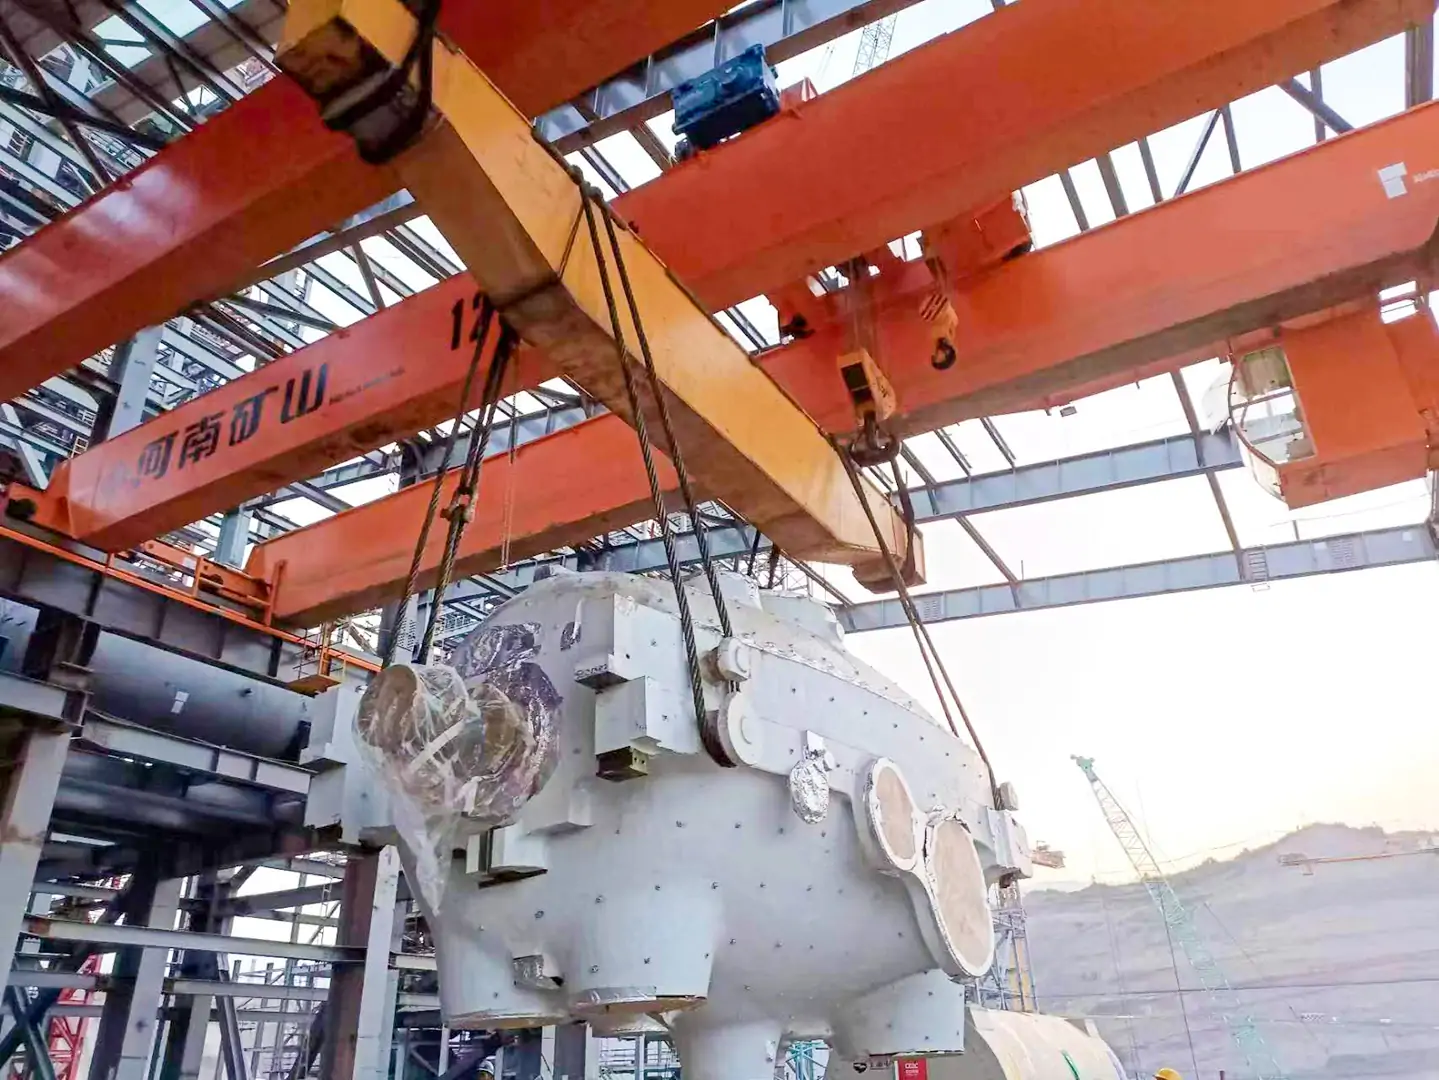
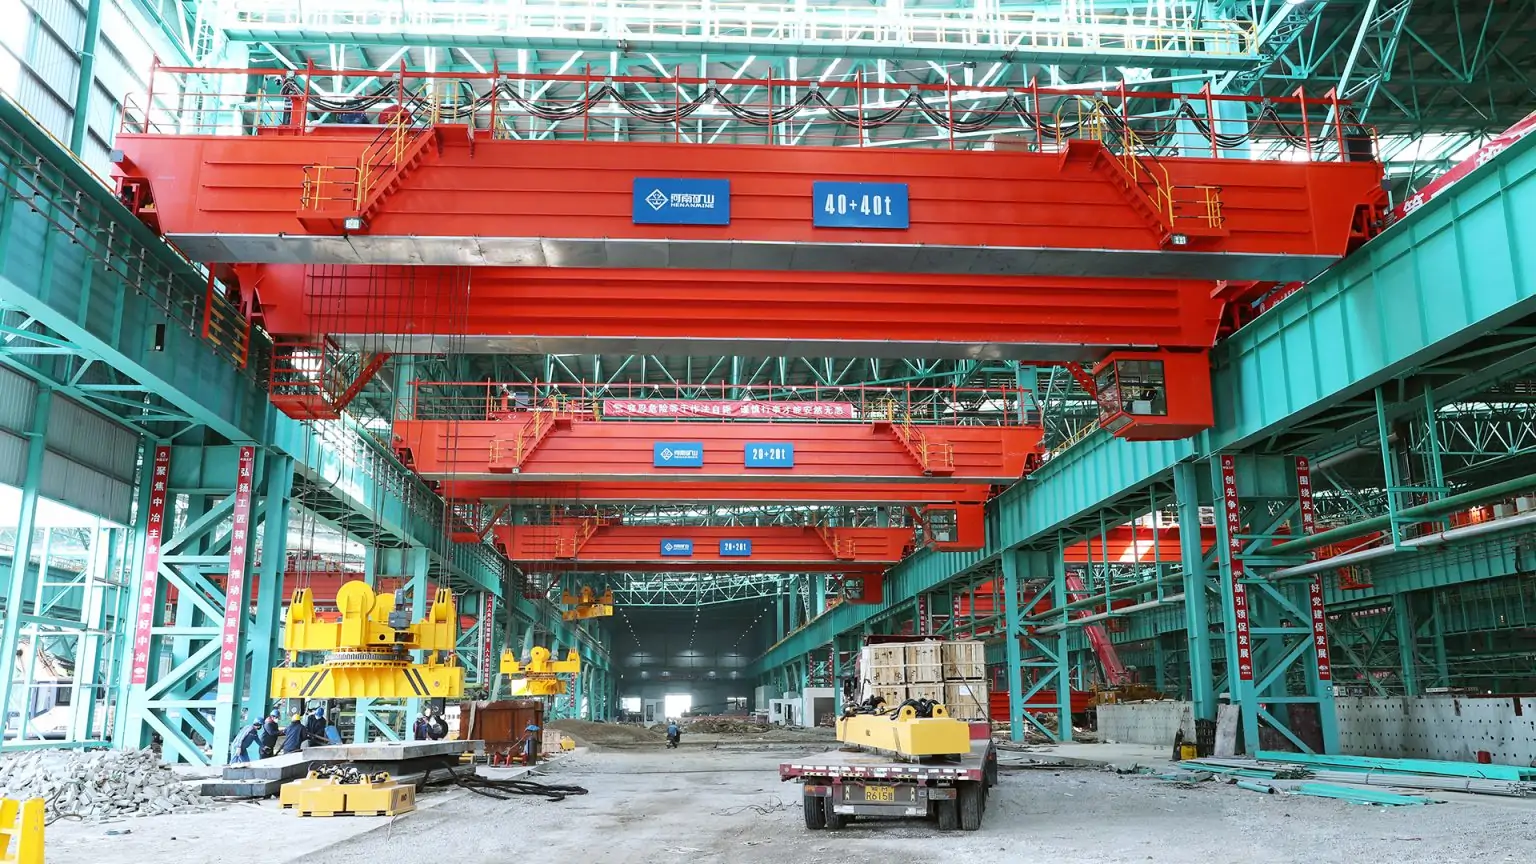
    120 ton double-girder overhead crane lifting generating-unit equipment in a thermal power plant
    A turbine-hall crane supports both generating-unit erection and future maintenance access.
    MAIN LIFTTurbine-Hall Bridge Crane
    BULK HANDLINGCoal Grab Crane
    SERVICE AREASBoiler, Mill and Workshop
    DESIGN BASISErection and Overhaul Loads

    What Is a Thermal Power Plant Crane?

    A thermal power plant crane is a lifting system specified for a defined area of a coal-fired, gas-fired, biomass or cogeneration facility. In the turbine hall, an overhead traveling crane installs and later handles generator and turbine components. Fuel-handling buildings may use grab cranes for coal. Boiler, mill, pump and maintenance areas often require smaller bridge cranes or local hoists.

    These applications have different load cases. A turbine-hall crane must reach every critical erection and overhaul position with sufficient lifting capacity and clearance. A coal grab crane is sized from bulk density, grab volume, hourly throughput and repeated operating cycles. A single generic crane specification cannot describe both duties reliably.

    Thermal Power Plant Crane Selection Considerations

    • Maximum suspended load: identify the generator stator, rotor, turbine casing and other heavy components; include the lifting beam, attachment and rigging in the load calculation.
    • Construction and maintenance: check the original unit erection plan and the future overhaul plan. The heaviest load and most difficult hook approach may occur at different stages.
    • Turbine-hall geometry: provide runway span and elevation, travel length, building section, delivery opening, hook approach and the complete lifting route.
    • Main and auxiliary hooks: define each hook’s load, speed, operating duty and permitted combined use.
    • Coal and ash properties: state bulk density, material temperature, dust exposure, required throughput and operating cycles before selecting a grab crane.
    • EPC schedule: coordinate drawing approval, runway readiness, crane delivery, erection, load testing and generating-unit installation.

    Thermal Power Plant Crane Systems Compared

    Crane system Power plant duty Primary selection factor Project interface
    Double-girder turbine-hall overhead crane Generator and turbine installation, rotor handling and overhaul Maximum suspended load, hook reach and controlled placement Runway loads, main and auxiliary hooks, building clearance
    Single- or double-girder maintenance crane Boiler, pump and auxiliary-equipment areas Component load, headroom and service frequency Local building support and maintenance access
    Four-rope grab overhead crane Coal or other suitable bulk-material handling Bulk density, grab payload and cycles per hour Dust control, hopper positions and material temperature
    Cross-travel overhead crane Coal-mill equipment transfer across connected bays Equipment route and track-switching arrangement Runway connection and control logic
    Double-girder gantry crane Outdoor component receiving and laydown Heavy-lift route, span and outdoor duty Foundations, wind limits and power supply

    Selection rule: specify the turbine hall from the most demanding erection and overhaul lift; specify a grab crane from material throughput and operating duty. These are separate procurement packages.

    Crane Duties Across the Power Plant

    Plant area Typical load Critical consideration
    Turbine hall Generator stator, rotor, turbine casing and major assemblies Main-hook capacity, lifting height, hook approach and precision control
    Boiler and feedwater areas Fans, pumps, valves and service modules Restricted headroom, access openings and hot surfaces
    Coal-handling building Raw coal between storage and transfer positions Grab payload, dust, cycle time and fire protection
    Ash and slag area Bulk material where crane handling is required Temperature, abrasion, corrosion and grab suitability
    Outdoor laydown yard Large delivered components and maintenance assemblies Foundation capacity, travel route and weather conditions
    double-girder grab overhead crane for coal and bulk material handling
    Fuel-handling cranes require a grab and operating duty matched to the material and transfer process.

    Turbine-Hall Crane Engineering

    The heaviest load may be lifted during generator installation, while the most difficult hook position may be required during rotor extraction years later. The crane general arrangement should show every critical pickup and set-down position in plan and section.

    Design item Required project information
    Rated lifting capacity Component mass plus lifting beam and rigging; main and auxiliary hook load cases
    Hook coverage Runway span and length, approach dimensions, pickup elevation and required set-down positions
    Runway and building Maximum wheel loads, horizontal forces, rail tolerances, access and erection method
    Motion control Normal travel speed, minimum controllable positioning speed, braking and fault response
    Maintenance Walkways, inspection points, electrical isolation, equipment removal route and spare parts

    If two cranes are intended for a tandem lift, the lift plan must check unequal load sharing, combined runway reactions, coordinated operation and a safe response to a fault. Two independent cranes do not automatically provide tandem-lift capability.

    Published Henan Mine Crane Product Ranges

    These published product-family ranges support early selection. A final power plant crane specification requires the verified load cases, operating duty and site drawings.

    Product family Capacity Span Lifting height / duty Relevant area
    Electric-hoist double-girder bridge crane 3–32 t 7.5–31.5 m 6–30 m; A3–A5 Auxiliary maintenance bays
    Four-rope grab bridge crane 5–50 t 10.5–31.5 m 6–30 m; A6–A8 Approved coal and bulk-material duties
    Cross-travel overhead crane 1–32 t 3–30 m 4–20 m; A5–A6 Coal-mill maintenance transfer
    MG double-girder gantry crane 5–500 t broad family 8–40 m 6–30 m; A3–A8 broad family Outdoor laydown and equipment transfer

    The Indonesian 120 t turbine-hall crane is a separate project reference. Its capacity must not be treated as the standard requirement for every generating unit.

    Project Reference: Two 120 t Cranes in Indonesia

    For a thermal power project in Morowali, Central Sulawesi, Indonesia, Henan Mine Crane reports supplying two 120 t double-girder bridge cranes. The cranes supported the installation of three 380 MW supercritical coal-fired generating units. Heavy equipment handling, smooth movement and controlled positioning were central requirements.

    This project demonstrates a turbine-hall application. A different plant requires its own stator and rotor weights, rigging plan, hall dimensions, hook approach and runway calculations before selecting capacity. View the published thermal-power project account.

    120 ton Henan Mine Crane bridge crane lifting equipment at an Indonesian thermal power project
    Published project photography of generating-unit equipment handling in the turbine-hall construction area.

    Thermal Power Plant Crane Price and Budget

    The figures below are public equipment-level planning references in US dollars. They are not an installed power plant price or a Henan Mine Crane quotation for the Indonesian project.

    Published source Stated configuration Equipment price reference Comparison limit
    Henan Mine Crane 2026 market guide 20 t double-girder overhead crane US$22,000–60,000 General crane benchmark for an auxiliary area
    Henan Mine Crane 2026 market guide 30–50 t heavy double-girder class US$35,000–130,000+ Broad equipment range; not an installed turbine-hall price
    DGCRANE manufacturer price list 50/10 t, 10.5–31.5 m, A5–A6 US$49,500–72,000 Another supplier’s equipment reference
    DGCRANE manufacturer price list 100/20 t, 13–31 m, A5–A6 US$115,000–166,700 High-capacity comparison; not a 120 t quotation
    120 t Indonesian thermal-power project Two double-girder cranes Project quotation required No comparable public transaction price was verified

    Price sources: Henan Mine Crane, “2026 Overhead Crane Price Guide”; DGCRANE, “Top Running Overhead Crane” price list. Public ranges may change with the final specification.

    Total installed cost: separate crane equipment, lifting beam, runway steel, power supply, freight, import charges, erection, commissioning, load testing, training and spare parts in the commercial schedule.

    Dust, Heat and Safe Operation

    The turbine hall, coal building and ash system have different operating environments. Specify ambient and radiant temperature, dust, humidity, corrosion and cleaning practice separately for each area. Electrical enclosure ratings and protective features should follow the actual site classification.

    • Coal and ash: confirm bulk density, grab payload, material temperature, abrasion and dust containment.
    • Hazardous locations: identify any formally classified area before specifying explosion-protected equipment.
    • Load protection: define overload limits, brakes, emergency stops, travel limits and recovery from power or drive faults.
    • Maintainability: provide access to the hoist, trolley, electrical system and crane runway after the generating units are installed.
    • Acceptance: agree factory inspection, site alignment, functional testing, load tests, operating records and training before handover.

    Thermal Power Plant Crane RFQ Checklist

    A technical proposal and comparable quotation require:

    • Project country, generating-unit type and capacity, applicable standards and EPC milestones.
    • Heaviest erection and overhaul loads, dimensions, lifting points, center of gravity, lifting-beam and rigging weights.
    • Turbine-hall plan and section, runway span and length, rail elevation, hook approaches and delivery route.
    • Main and auxiliary hook duties, lifting height, normal and precision speeds, control method and power supply.
    • Existing or proposed runway structure, allowable wheel loads and installation access.
    • For bulk handling: material type, bulk density, grab volume, throughput and cycles per hour.
    • Required scope for freight, installation, commissioning, training, spare parts, warranty and local service.

    Thermal Power Plant Crane FAQ

    What crane is used in a turbine hall?

    A double-girder overhead traveling crane is commonly selected for heavy generator and turbine installation and later overhaul. Its capacity and hook arrangement follow the verified plant lifting plan.

    How is turbine-hall crane capacity determined?

    Check the maximum component mass together with lifting-beam and rigging weight. Then verify hook combinations, runway reactions, clearances, duty and the approved lifting method.

    Does every 380 MW unit require a 120 t crane?

    No. The Indonesian project is one 120 t reference. Another unit must be sized from its own equipment loads and erection and overhaul plan.

    What does a 120 t power plant crane cost?

    A project quotation requires the main and auxiliary hook ratings, span, lifting height, controls, runway interface, destination and installation scope. A published 100/20 t equipment price cannot be presented as the price of a 120 t power plant system.

    Can a coal grab crane replace the turbine-hall crane?

    No. The grab crane is designed for repeated bulk-material cycles. The turbine-hall crane handles large suspended machinery and controlled positioning.

    Related Henan Mine Crane Products

    double-girder overhead crane for turbine-hall lifting

    Double-Girder Overhead Crane

    Heavy bridge-crane platform for generating-unit installation and overhaul.

    View Product →

    electric-hoist double-girder crane for power plant maintenance bay

    Electric Hoist Double-Girder Crane

    Equipment handling in auxiliary and maintenance bays.

    View Product →

    four-rope grab overhead crane for power plant coal handling

    Grab Double-Girder Overhead Crane

    Repetitive handling of coal and other suitable bulk materials.

    View Product →

    cross-travel overhead crane for coal-mill maintenance

    Cross Travel Overhead Crane

    Transfer of maintenance equipment between connected bays.

    View Product →

    double-girder gantry crane for power plant outdoor laydown yard

    Double-Girder Gantry Crane

    Outdoor staging and transfer of large components.

    View Product →

    5 ton overhead crane for power plant component maintenance

    5 Ton Overhead Crane

    Local service lifting for smaller pumps, valves and assemblies.

    View Product →

    Henan Mine Crane · Technical basis: published product specifications and project account · Source check: 2026

    Request a Thermal Power Plant Crane Proposal

    Send the generating-unit load list, turbine-hall drawings, coal-handling process data and EPC schedule. Henan Mine Crane can prepare an equipment configuration and itemized technical and commercial proposal for each plant area.

    Henan Mine CraneDiscuss your requirements ↗
  • Steel Warehouse Crane Systems

    Steel Warehouse Crane Systems

    Steel Warehouse Crane Systems

    Henan Mine Crane · Steel Storage and Distribution Systems

    Steel Warehouse Crane Systems

    Overhead, gantry, magnetic, rotating-beam and automated crane systems for receiving, storing, locating, retrieving and dispatching steel plate, profiles, bars, pipe, coils, billets and finished products.

    Henan Mine Crane configures each steel warehouse crane from the complete material master, gross suspended load, storage geometry, throughput, lifting attachment, building or stockyard interface, control level, safety strategy and required data exchange.

    automated steel warehouse crane above organized steel plate storage positions
    A steel warehouse crane is engineered around the complete storage and dispatch process, including load identification, stack allocation, controlled placement and inventory traceability.

    MATERIALS

    Plate, Profiles, Bars, Pipe & Coils

    CRANE TYPES

    Bridge, Magnetic, Rotating & Gantry

    CONTROL LEVELS

    Manual, Assisted & Automatic

    PROJECT BASIS

    Load, Flow, Layout, Duty & Data

    What Is a Steel Warehouse Crane?

    A steel warehouse crane is an application-specific material-handling system that transfers steel between receiving, inspection, storage, production supply, order picking and dispatch. Unlike a general workshop crane selected mainly by capacity and span, a warehouse system must also control long-load orientation, stack access, material identity, storage location, retrieval sequence and the interface with trucks, rail wagons, conveyors or processing lines.

    The term does not describe one fixed machine. A light indoor warehouse may use a compact single-girder overhead crane. Intensive plate storage may use a double-girder electromagnetic crane with a rotating beam. Long nonmagnetic or coated products may require two hooks, two trolleys or a purpose-designed spreader. Outdoor stockyards commonly use a gantry crane with wind protection and ground-supported rails.

    Henan Mine Crane combines its single-girder bridge crane, double-girder bridge crane, magnetic lifting, double-trolley and gantry crane platforms with warehouse positioning, sensing and data functions selected for the declared process.

    Steel Warehouse Material Flow

    Crane coverage and storage logic should follow the complete route of every approved material family. Omitting an interface normally creates extra floor handling, unidentified stock or an unsafe manual recovery step.

    1. Receiving and Unloading

    Unload trucks or rail wagons within the permitted vehicle envelope, verify gross load and product identity, and place incoming steel in inspection or assigned buffer positions.

    2. Identification and Inspection

    Confirm material ID, heat number, grade, dimensions, weight, surface condition and release status before the storage location is recorded.

    3. Storage Allocation

    Assign a stack, cassette, rack or floor cell from product dimensions, grade, turnover, dunnage, stack-height limits and retrieval priority.

    4. Controlled Placement

    Position the load without striking adjacent stacks, racks, columns, vehicles or people, while maintaining required orientation and layer separation.

    5. Retrieval and Production Supply

    Retrieve the specified item or bundle, manage reshuffling where required and deliver it to cutting, fabrication or order-staging positions.

    6. Dispatch and Reconciliation

    Stage and load the shipping order, confirm the final vehicle handoff and update inventory only after the physical movement is completed and verified.

    steel plate storage warehouse served by an overhead handling system
    Warehouse design coordinates crane travel, storage cells, inbound and outbound bays, process interfaces and inventory records.

    Steel Warehouse Crane System Architecture

    1. Crane structure and runway: transfer vertical, longitudinal, transverse and dynamic reactions to the building or foundations while providing full required coverage.
    2. Hoist, trolley and travel drives: provide the declared capacity, lift, speed range, positioning control, braking and duty classification.
    3. Load attachment: connects to plate, profiles, pipe, coils or bundles through a magnet, rotating magnetic beam, hook, spreader, clamp, tong, C-hook or custom device.
    4. Sensing and protection: may include load, position, height-profile, skew, anti-collision, obstacle, access-gate, vehicle-presence and restricted-zone functions.
    5. Control system: coordinates pendant, radio, cabin, assisted or automatic operation, including mode selection, safe stopping and manual recovery.
    6. Warehouse data interface: exchanges material identity, location, movement order, completion status, alarms and reconciliation records with WMS, MES or ERP systems.
    warehouse crane machinery and controls above steel storage stacks
    The mechanical crane, lifting attachment, sensing, controls, warehouse data and civil interfaces must be specified as one operating system.

    Rated-load basis: the maximum gross suspended load includes the steel product, lifting magnet, magnetic or mechanical beam, clamps, slings, shackles, C-hook, hook block and every suspended accessory. Eccentric loading, unequal pickup, retained moisture, stacked layers and any permitted rotation or load-turning case also require evaluation.

    Steel Warehouse Crane Selection Considerations

    Selection starts with the full material and movement database. Capacity alone cannot establish attachment suitability, long-load stability, storage density, cycle performance or structural reactions.

    Material Master

    Mass, length, width, thickness, diameter, section, center of gravity, ferromagnetic response, surface, coating, temperature, stiffness, nesting and permitted pickup points.

    Throughput and Duty

    Inbound and outbound tonnes, moves per hour, starts, average and peak travel, shifts, annual hours, load spectrum, reshuffle ratio, availability target and maintenance window.

    Storage Geometry

    Stack, rack or cassette dimensions; stack height; dunnage; aisle; approach clearance; floor loading; reserved zones; vehicle bays and future expansion.

    Attachment and Orientation

    Magnetic eligibility, single- or multi-layer lift, required rotation, hook spacing, clamp locations, coil axis, pipe support, allowable deflection and changeover method.

    Building or Stockyard

    Span, runway length and elevation, lift, headroom, end and side approaches, rail and beam data, wheel-load limits, foundations, wind, drainage and installation access.

    Control and Acceptance

    Manual, assisted or automatic mode; warehouse interface; positioning and cycle criteria; exception recovery; safety functions; standards; inspection route and measurable handover tests.

    Steel Warehouse Crane Configurations Compared

    Crane configuration follows the material family, operating intensity, orientation requirement, building interface and attachment. Automation is a control and data layer that can be applied to several structural configurations; it is not a substitute for correct mechanical selection.

    Configuration Typical Application Principal Advantages Points Requiring Definition
    Single-Girder Overhead Crane General indoor hook handling at lighter capacity and moderate duty. Compact structure, lower self-weight and efficient use of workshop space. Headroom, hook approach, hoist duty, long-load control and building reactions.
    Double-Girder Overhead Crane Heavier loads, intensive service, longer spans or process attachments. Higher structural capability and greater flexibility for trolleys, platforms and controls. Wheel loads, access, maintenance clearances, attachment mass and required duty class.
    Electromagnetic Bridge Crane Repetitive handling of validated ferromagnetic plate, profiles or billets without load rotation. Fast pickup without manual sling placement and efficient handling of approved product families. Magnetic test basis, air gap, layer control, backup power, retained-load response and exclusion zone.
    Rotating Magnetic-Beam Crane Plate or long steel that must rotate between vehicle, storage and process orientations. Combines magnetic pickup with controlled orientation and dense storage access. Rotation envelope, load overhang, cable management, stack clearance and collision zoning.
    Double-Trolley or Two-Hook Crane Long, flexible, nonmagnetic, coated or mixed steel products requiring two support points. Variable support spacing and mechanical handling across diverse load families. Capacity split, load sharing, synchronization, skew, permitted independent motion and lift plan.
    Gantry Crane Outdoor steel stockyards, loading areas or buildings without a suitable runway structure. Ground-supported coverage with optional cantilevers for vehicle lanes. Wind actions, storm anchoring, rail and foundation design, drainage, travel path and outdoor protection.

    Mixed inventory: warehouses storing plate, profiles, coils and finished fabrications may require more than one attachment or more than one crane. Changeover time, attachment storage, interlocks and rated-load changes must be included in the operating concept.

    Published Crane Platform Ranges

    The following Henan Mine Crane product-page ranges provide an initial platform reference. They are not a universal warehouse specification. Final capacity, span, lift, duty, speeds and attachment are selected from the actual load case and operating cycle.

    Published Platform Published Capacity Published Span Published Lift Published Class
    European-Style Electric Single-Girder Crane 1–10 t 7.5–28.5 m 6–30 m A3–A5
    Intelligent Electric Hoist Overhead Crane 1–32 t 7.5–31.5 m 6–30 m A5–A6
    Electromagnetic Bridge Crane 5–32 t, including magnet weight 10.5–31.5 m 6–30 m A1–A8 published range; duty selected by project
    Upper Rotating Magnetic Overhead Crane 5+5 to 25+25 t 10.5–31.5 m 6–20 m A6–A7
    Electromagnetic Hanging Crane 5–50 t 10.5–31.5 m 6–20 m A6–A7
    Double-Trolley Electric Hoist Overhead Crane 1+1 to 32+32 t 7.5–31.5 m 6–30 m A5–A6
    Single-Girder Gantry Crane 1–32 t 6–35 m 4–20 m A3–A5

    Lifting Attachments for Warehouse Steel

    No single attachment safely handles every steel product. The approved attachment schedule should identify each load family, pickup method, rated capacity, inspection requirement, prohibited condition and storage position.

    Attachment Common Warehouse Loads Engineering Checks
    Hooks, Slings and Spreader Beam Mixed products, bundles, fabricated steel and approved lifting points. Sling angle, edge protection, balance, support spacing, bend radius and manual access.
    Plate Clamps Single plate within the clamp’s approved thickness, hardness, orientation and surface range. Clamp model, minimum load, jaw condition, plate edge, number of clamps and permitted lifting direction.
    Magnet or Magnetic Beam Validated ferromagnetic plate, billet, profiles and selected bundles. Material response, thickness, flatness, air gap, coating, scale, temperature, layer control and retained-load plan.
    Rotating Magnetic Beam Long plate and profiles requiring controlled horizontal orientation. Overhang, rotation radius, cable routing, adjacent stacks, skew and travel interlocks.
    C-Hook or Coil Tong Eye-horizontal or eye-vertical coils within the specified ID, OD and width range. Coil orientation, telescoping risk, counterweight, protection pads, clearance and attachment self-weight.
    Pipe Beam, Cradle or Tongs Pipe, tube and round stock in approved single pieces or bundles. Rolling restraint, bundle integrity, support distance, coating protection and end clearance.
    upper rotating magnetic overhead crane for long steel storage
    A rotating magnetic system is considered when load orientation changes between incoming transport, storage lanes and downstream equipment.
    double trolley overhead crane for long steel warehouse loads
    Two lifting points can support long products when magnetic handling is unsuitable or when adjustable hook spacing is required.

    Magnetic Load Integrity and Power-Loss Planning

    Electromagnetic handling is suitable only after the actual load range is validated. Magnetic grade, plate thickness, contact area, flatness, rust, mill scale, paint, protective film, oil, temperature and gaps between stacked products can all change holding force. A successful pickup of one plate does not validate another thickness, surface or multi-layer condition.

    • Define every approved material and surface condition, including minimum thickness and maximum air gap.
    • State whether single-sheet selection, multiple-sheet lifting or bundle lifting is permitted.
    • Include magnet, beam and cable-reel mass in crane capacity and structural reactions.
    • Specify power-loss behavior, retained-load indication, backup-energy duration and the emergency landing process.
    • Segregate suspended-load routes from people and control access to loading, storage and recovery zones.
    electromagnetic hanging beam crane handling long steel material
    Magnet selection and emergency response are based on tested load families, not nominal steel weight alone.

    Manual, Assisted and Automated Warehouse Operation

    Operating Level Movement Control Inventory Control Application Conditions
    Manual Operator controls all crane motions by pendant, radio or cabin. Location updates are manual or scanner-assisted. Variable work, lower movement volume and clear visibility with disciplined procedures.
    Assisted Operator initiates the move; positioning, anti-sway or protected approach functions assist execution. Movement orders and confirmations exchange with warehouse software. Repeatable lanes with exceptions that still require frequent operator judgment.
    Automatic PLC or supervisory control executes validated routes, pickup, transfer and placement sequences. WMS, MES or ERP issues tasks and receives location, completion and exception records. Defined inventory, controlled geometry, measurable interfaces and formal exception recovery.

    Automation Data and Acceptance Criteria

    A warehouse movement record normally carries material ID, heat number, grade, dimensions, weight, storage cell, stack layer, status, order number and time stamps. The functional design also defines duplicate IDs, missing labels, mismatched weight, occupied positions, blocked routes, sensor failure, communication loss and manual recovery.

    Contract acceptance should use measurable criteria such as representative-load cycle time, positioning tolerance, correct item and location confirmation, interface response, alarm handling, safe-state behavior, recovery time and sustained trial performance. Values are established for the specific layout and process rather than assumed from a generic crane.

    automated crane monitoring and steel warehouse control interface
    Automation scope includes data quality, task execution, safety states, exception handling and controlled manual recovery.

    Warehouse Layout, Runway and Civil Interfaces

    Coverage and Approaches

    Confirm rail-center span, runway length, hook and attachment approaches, loading-bay reach, cantilever coverage and positions inaccessible to the selected attachment.

    Vertical Envelope

    Coordinate rail elevation, crane depth, upper clearance, hook lift, beam or magnet depth, product height, stack height, vehicle height and maintenance access.

    Structural Reactions

    Provide maximum and minimum wheel loads, lateral and longitudinal forces, buffer loads, fatigue basis and rail tolerances for building, runway or foundation verification.

    Vehicle and People Separation

    Define loading zones, pedestrian routes, gates, barriers, warning devices, travel interlocks and the process for driver positioning during crane operation.

    Stack and Floor Design

    Confirm floor bearing, rack or dunnage capacity, stack stability, load distribution, drainage and the consequences of placing products in an incorrect cell.

    Outdoor Conditions

    For stockyards, specify operating and parked wind, storm anchoring, lightning, precipitation, corrosion, temperature, rail drainage and travel-path maintenance.

    long-span warehouse overhead crane with rotating magnetic lifting beam
    Attachment size, rotation envelope and stack layout often govern warehouse clearances more strongly than the hook block alone.

    Safety, Standards and Acceptance

    The project specification should state the governing jurisdiction, standards and editions. A common basis may include ISO 4301 for classification; EN 13001 and EN 15011 for crane design; EN 13155 for non-fixed load lifting attachments; or CMAA 70 with the applicable ASME B30.2, ASME B30.20 and ASME BTH-1 requirements. Electrical equipment may reference IEC 60204-32. Safety-related control design for automated functions may use ISO 13849-1 or IEC 62061 where applicable. Local statutory requirements and the signed contract remain controlling.

    Design Review

    Approve load cases, classification, structural and mechanism calculations, wheel loads, attachment logic, electrical architecture, safety functions and interface responsibility.

    Factory Verification

    Verify manufacturing records, material traceability, weld and nondestructive inspection scope, mechanism operation, control logic, alarms and documentation before shipment.

    Site Acceptance

    Check runway geometry, motions, brakes, limits, overload protection, collision functions, attachment performance, representative loads, proof load and agreed cycle scenarios.

    Operational Readiness

    Complete training, inspections, rescue and recovery procedures, attachment registers, preventive maintenance, critical spares, backup and restore, and change-control records.

    Operational boundary: no person should stand or pass under a suspended steel load. Automated operation requires controlled access, defined safe states and a documented method for removing or landing a retained load after a fault.

    Published Steel Plate Warehouse Automation Reference

    Henan Mine Crane has published a specialized crane reference for a steel plate storage facility serving steel-structure, bridge and high-rise fabrication. The official project account states that full-function verification was performed on a 1,200 t crane test platform before delivery to a major steel-structure company.

    Published project data identifies a 5–50 t structural range with span and lift customized to the warehouse. The delivered system reportedly managed more than 200 plate specifications. After more than one year of operation, the official reference reports a 65% increase in inbound and outbound efficiency, inventory error below 0.1% and annual labor savings exceeding RMB 1.2 million.

    The application links physical plate movements with storage-location and production-order data, illustrating the value of designing the crane, attachment, control logic and warehouse software interface as one project.

    published automated steel plate warehouse crane installation
    Published reference: specialized steel plate storage crane and warehouse automation project.

    Evidence boundary: these figures are attributed to one official published project reference. They demonstrate a delivered application but do not define the performance, savings or acceptance criteria of another warehouse. Project outcomes depend on material mix, baseline process, layout, operating discipline, interfaces and contracted scope.

    Steel Warehouse Crane Price and Budget Scope

    A steel warehouse crane price cannot be established from capacity alone. Public equipment listings are useful only as broad market references because complete projects may also require a lifting beam or magnet, backup power, runway, electrification, controls, WMS interface, freight, installation, testing, training and civil work.

    The public market review below was completed on 20 September 2026. Prices may change. Marketplace technical fields can be incomplete or internally inconsistent, so every capacity, span, attachment and supply boundary requires confirmation in a signed proposal.

    Public Reference Displayed Price Displayed Scope Commercial Boundary
    Henan Mine Crane supplier marketplace listing: 8 t workshop/warehouse bridge crane US$4,000 per piece; MOQ 1 Configurable equipment listing Qingdao is the displayed port; freight, destination scope and inconsistent listing fields require written confirmation.
    Henan Mine Crane supplier marketplace listing: 20 t electromagnetic overhead crane US$3,099–18,888 per set; MOQ 1 Configurable electromagnetic crane listing Final magnet, beam, backup energy, capacity, span, duty and project inclusions are not established by the displayed range.
    Bohl Crane public listing: Yale 10 t top-running single-girder crane kit US$28,500 Crane kit with hoist Published exclusions include bridge beams, runway rails, runway conductor bar, fabrication and installation.
    Complete automated steel plate warehouse crane project Project-specific quotation Crane, attachment, sensing, controls, data interface and site scope Requires load database, throughput model, layout, runway data, interface specification, acceptance plan and delivery destination.

    Reference sources: public Henan Mine Crane supplier listings on Made-in-China and the Bohl Crane online store. These third-party prices are market observations, not quotations or offers from this page.

    Main Cost Drivers

    Crane Mechanics
    Capacity, span, lift, duty, speed, reeving, trolley arrangement and access.
    Load Attachment
    Magnet, rotating beam, clamps, C-hook, spreader, cable reel and backup energy.
    Controls and Data
    Variable-frequency drives, sensing, anti-sway, positioning, PLC, HMI and WMS integration.
    Runway and Site
    Rails, beams, columns, foundations, electrification, access, erection and load testing.
    Compliance
    Design code, documentation, inspection, certification, special environment and local requirements.
    Delivery Scope
    Incoterm, freight, duties, installation, commissioning, training, spares and warranty support.

    Engineering and Procurement Deliverables

    A comparable procurement package separates technical performance from commercial scope. The following deliverables should be identified in the enquiry and proposal.

    Design Basis

    Load matrix, duty calculation, process description, governing standards, environment, reliability basis, safety functions and exclusions.

    Interface Drawings

    General arrangement, wheel loads, clearances, runway and rail data, power points, communication interface, foundation actions and installation access.

    Attachment Schedule

    Approved products, ratings, pickup conditions, prohibited conditions, changeover, inspection, power-loss response and attachment parking.

    Control Description

    Operating modes, sequences, interlocks, alarms, safe states, warehouse handshake, access control, event history and fault recovery.

    Inspection and Test Plan

    Hold points, material and weld records, factory tests, site tests, proof load, representative-load scenarios, interface tests and acceptance criteria.

    Lifecycle Package

    Manuals, drawings, parts list, certificates, training, preventive maintenance, critical spares, diagnostic access, backup files and support responsibility.

    Information Required for a Steel Warehouse Crane Quote

    Complete enquiry data allows mechanical, structural, attachment, control and commercial scope to be evaluated on one defined basis.

    Material and Load File

    Product family, material grade, minimum and maximum mass, dimensions, center of gravity, surface, temperature, bundle condition, attachment and gross suspended load.

    Movement and Throughput

    Inbound, storage, reshuffle, retrieval and outbound routes; moves per hour; tonnes per shift; load spectrum; peak schedule; availability and maintenance window.

    Warehouse Layout

    Plan, cross-section, span, runway length and elevation, storage cells, stacks, racks, aisles, vehicle bays, process interfaces, clearances and expansion zones.

    Existing Structure or Foundations

    Rail section, beams, brackets, columns, foundations, wheel-load limits, condition assessment, geometry survey, power supply and erection access.

    Controls and Warehouse Interface

    Operating modes, required speed and positioning, sensors, anti-collision, WMS or ERP protocol, material fields, cybersecurity responsibility, exceptions and recovery.

    Commercial and Compliance Scope

    Destination, standards, Incoterm, freight, runway, installation, commissioning, inspection, load test, training, spares, documentation, warranty and target schedule.

    Fastest route to a comparable proposal: submit a warehouse plan and cross-section, load spreadsheet, process-flow arrows, attachment preference, throughput target, runway data and required supply boundary. Open points can then be recorded explicitly instead of being hidden inside an assumed price.

    Frequently Asked Questions

    Which crane type is suitable for a steel warehouse?

    Single-girder cranes serve lighter general handling. Double-girder cranes suit heavier or intensive duty. Magnetic cranes support validated ferromagnetic loads, rotating systems control orientation, double-trolley cranes support long loads and gantry cranes serve outdoor stockyards.

    How is steel warehouse crane capacity calculated?

    Capacity starts with the maximum gross suspended load: steel product plus magnet, beam, clamps, slings, C-hook, shackles, hook block and every accessory. Eccentric load, unequal pickup and dynamic cases are then evaluated.

    Can one magnet lift every steel plate?

    No. Magnetic grade, thickness, flatness, coating, rust, scale, temperature, air gap and number of layers affect holding force. Each approved plate family and pickup condition requires validation.

    When is a rotating magnetic beam required?

    Rotation is considered when long steel arrives in one orientation but must be stored, processed or loaded in another. The design must include the complete rotation envelope and adjacent-stack clearance.

    Can an existing warehouse runway be reused?

    Only after rails, beams, brackets, columns, connections and foundations are checked for condition, geometry, fatigue and the proposed vertical, lateral, longitudinal and dynamic reactions.

    Does warehouse automation require a new ERP?

    Not necessarily. The required material fields, task handshake, ownership of location data, error codes, recovery process and communication protocol determine whether an existing WMS, MES or ERP can interface with the crane control system.

    How much does a steel warehouse crane cost?

    Public references reviewed in September 2026 ranged from US$4,000 for one configurable 8 t equipment listing to US$28,500 for a 10 t crane kit, while a complete automated warehouse remains quotation-based. These scopes are not directly comparable.

    What should be tested before handover?

    Testing should cover motions, brakes, limits, overload protection, attachment performance, power-loss response, representative products, protected zones, inventory transactions, alarms, manual recovery, proof load and contracted cycle scenarios.

    Request a Steel Warehouse Crane Quote

    Submit the material list, maximum gross suspended load, warehouse layout, span, lift, movement frequency, attachment preference, control level, destination and required delivery scope. Henan Mine Crane will prepare a configuration and commercial proposal against the declared operating basis.

    Henan Mine CraneDiscuss your requirements ↗
  • Steel Mill and Foundry Cranes

    Steel Mill and Foundry Cranes

    Steel Mill and Foundry Cranes

    Henan Mine Crane · Steel Production Lifting Systems

    Steel Mill and Foundry Cranes

    Henan Mine Crane engineers steel mill and foundry cranes for raw-material handling, furnace charging, molten-metal transfer, continuous casting, hot rolling, slab and billet movement, coil and plate storage, scrap handling and plant maintenance. Each crane is matched to its process load, attachment, heat exposure, production cycle, runway and required safe-failure response.

    A complete steelworks normally requires several crane types rather than one universal design. Ladle cranes prioritize molten-metal safety; magnetic and clamp cranes protect finished material; grab cranes handle bulk feed and slag; maintenance cranes provide controlled access to production equipment. The plant crane schedule must therefore be developed bay by bay and duty by duty.

    Henan Mine Crane metallurgical overhead crane operating in a steel mill
    Metallurgical overhead crane configured for high-duty material transfer and integration with steel-production operations.

    PROCESS COVERAGE

    Melt Shop to Finished Stock

    CRANE FAMILIES

    Hook, Ladle, Magnet, Grab and Clamp

    LISTED CAPACITY COVERAGE

    5–500 t, Model-Dependent

    WORKING CLASS

    A6–A8, Model-Dependent

    Steel Mill and Foundry Crane Systems by Process Area

    Steel mill cranes are process-specific overhead lifting systems used throughout ironmaking, steelmaking, casting, rolling, storage and maintenance. Foundry cranes form the high-risk molten-metal segment of this larger equipment family. The selected structure, hoisting mechanism, attachment, control method and protection package must correspond to the exact material and production step.

    Direct ladle handling cannot be specified in the same manner as billet storage or general maintenance. Likewise, a magnetic crane intended for flat plate requires different pickup geometry and loss-of-power protection from a grab crane moving slag or scrap. A dependable procurement package separates each duty before equipment selection begins.

    Raw Materials and Scrap

    Grab, magnet and dual-purpose cranes move scrap, ore, coke, flux, slag and other bulk or ferrous material.

    Melting and Pouring

    Charging, ladle and casting cranes support furnace feed, molten-metal transfer, treatment and controlled pouring.

    Casting and Rolling

    Slab, billet, bloom, coil and plate cranes transfer hot and finished material between process and storage zones.

    Maintenance and Assembly

    Heavy-duty hook cranes provide planned access to furnaces, rolls, motors, gearboxes, ladle cars and production equipment.

    Selection Considerations

    01 / MATERIAL

    Load Form and Temperature

    Identify molten metal, scrap, bulk feed, slag, slab, billet, coil, plate, mould or machinery; record normal and maximum temperature at pickup and travel.

    02 / LOAD

    Complete Suspended Mass

    Include payload, ladle or container, refractory lining, magnet, grab, clamp, lifting beam, rigging and all allowances required by the governing design basis.

    03 / PROCESS

    Production Route and Cycle

    Define pickup and set-down stations, travel distances, lifts per hour, near-capacity lifts, shift pattern, production interlocks and required cycle time.

    04 / ATTACHMENT

    Pickup and Release Method

    Confirm trunnion, hook, magnet, clamp, tong, C-hook, grab or beam interface, including rotation, opening, closing, power and safe-release requirements.

    05 / ENVIRONMENT

    Heat, Dust, Fumes and Splash

    Record ambient and radiant heat, conductive dust, scale, moisture, corrosive fumes, molten splash, outdoor exposure and enclosure requirements.

    06 / SAFETY

    Credible Failure Response

    Establish the required response to power loss, brake fault, drive failure, overspeed, overload, attachment power loss, upper-limit activation and control interruption.

    07 / RUNWAY

    Building and Rail Interface

    Verify span, lift, approaches, wheel loads, horizontal reactions, rail section, alignment, support capacity, thermal effects and erection access.

    08 / PROJECT SCOPE

    Controls, Standards and Supply Boundary

    Define cabin, radio or automation, power supply, plant communication, governing standard, inspection plan, documentation, freight and installation responsibilities.

    The crane name is not a complete specification. A magnetic plate crane, a ladle crane and a maintenance bridge crane can share the same rated capacity while requiring different duty classifications, attachments, brakes, controls, wheel loads and acceptance tests.

    Compare Steel Mill and Foundry Crane Types

    The preferred crane follows the production duty and handled material. This comparison provides an initial route from plant process to product family; final selection requires the complete operating and site data.

    Crane Type Handled Material Listed Product Range Critical Selection Point
    Double-Girder Foundry Crane Molten iron or steel ladles 50–150 t; 10–35 m span; A7–A8 Complete ladle mass, trunnion interface, heat exposure and molten-metal safety basis
    Four-Girder Casting Crane Ultra-heavy ladles and foundry loads 200/50–500/200 t; 10–40 m span; A7–A8 Main and auxiliary trolley functions, torsional load cases and runway reactions
    Metallurgical Bin Crane Charge boxes and furnace feed 5–50 t; 7.5–35 m span; A6–A7 Box geometry, opening and tipping method, furnace clearance and dust protection
    Rotating Magnetic Overhead Crane Billets, plates, bars and long steel 5+5–25+25 t; 10.5–31.5 m span; A6–A7 Material magnetic properties, beam geometry, rotation, power-loss holding and stacking orientation
    Slab Handling Crane Hot or ambient slabs and billets 20–150 t; 10–39 m span; A7–A8 Material temperature, pickup face, clamp or magnet response and storage geometry
    Grab Overhead Crane Ore, coke, flux, slag and selected scrap Project-configured Bulk density, lump size, abrasiveness, grab volume, fill factor and discharge control
    Quenching Crane Hot components for heat treatment Project-configured high-duty system Immersion timing, lifting speed, emergency recovery and bath geometry
    Double-Girder Maintenance Crane Rolls, motors, gearboxes and plant equipment Project-configured Heaviest maintenance lift, access path, headroom, precision and planned usage

    The ranges above identify separate Henan Mine Crane product families and do not represent every possible capacity–span combination. Final values follow structural calculation, mechanism selection, runway limits and the approved technical specification.

    Crane Coverage Across the Steel Production Process

    specialized overhead crane serving a hot rolled steel plant
    High-duty bridge crane developed around hot-rolling loads, radiant heat, cycle frequency and production-line clearances.

    Stockyard and Scrap Bay

    Grab and magnetic cranes unload, sort, blend and feed scrap or bulk material. Crane capacity must include the attachment, and throughput calculations must use the actual grab fill factor or magnet pickup condition.

    Melt Shop and Foundry

    Bin cranes charge furnaces, while foundry and casting cranes lift ladles, transfer liquid metal and support pouring. Molten-metal duty requires a defined safety architecture and thermal protection rather than a general-purpose crane specification.

    Continuous Casting and Rolling

    Slab and billet cranes move material between casting machines, cooling areas, reheating furnaces, rolling lines and intermediate storage. Pickup geometry, material temperature and cycle time determine the attachment and control system.

    Finishing and Dispatch

    Magnetic beams, clamps, tongs and C-hooks handle plate, long steel and coils. Finished-material protection, rotation, stack height, warehouse management interfaces and safe holding during power loss become primary design inputs.

    Load Attachments for Steel Mill and Foundry Cranes

    The attachment is part of the lifting system, not an accessory selected after the crane. Its mass, geometry, power source, control logic and failure response affect crane capacity, headroom, stability and acceptance testing.

    Ladle Beam or Gantry Hook

    Engages ladle trunnions for molten-metal lifting. Trunnion diameter, centres, ladle envelope, seating and inspection access require confirmation.

    Electromagnetic Beam

    Lifts ferrous plate, billet, bar or scrap. Material grade, thickness, temperature, air gaps and safe holding after power loss govern selection.

    Grab Bucket

    Handles ore, coke, flux, slag and bulk scrap. Density, lump size, abrasiveness, moisture and target throughput define grab type and volume.

    Clamp, Tong or C-Hook

    Supports slab, billet, plate and coil handling. Contact pressure, surface protection, centre of gravity and loss-of-power behavior must be defined.

    slab handling crane for steel mill material transfer
    Slab handling crane configured around material temperature, slab dimensions, storage pattern and the selected magnetic or mechanical attachment.

    Engineering Requirements for Metallurgical Duty

    Structural Load Cases

    Girders, trolley frames, end carriages, wheels and runway interfaces are assessed for lifted load, attachment, dynamic effects, off-centre positions, skew forces and applicable thermal conditions.

    Mechanism Duty

    Motors, gearboxes, brakes, drums, ropes, sheaves, bearings and wheels are selected from starts, operating time, load spectrum, travel distances and production criticality.

    Thermal and Environmental Protection

    Heat shields, protected cables, metallurgical-duty motors, ventilated cabinets, insulated cabins, dust-resistant enclosures and temperature monitoring are applied where the measured exposure requires them.

    Safe-Failure Architecture

    Multiple brakes, redundant drives, drum brakes, backup power, magnet holding, limits, overload protection and emergency placement can be specified when required by risk and governing rules.

    Motion and Positioning

    Variable-frequency control, creep speed, anti-sway, encoders, coordinated drives and automatic positioning support stable ladle movement and repeatable material stacking.

    Plant Integration

    PLC and HMI systems can exchange task, position, load, alarm and status data with plant controls, warehouse systems or manufacturing execution systems under an agreed interface specification.

    Safety functions must be specified by function, independence, setpoint, alarm, stop category, recovery method and verification test. A component name alone does not establish suitability for molten metal or continuous steel-production duty.

    Steel Mill Crane Specification Schedule

    A plant-wide inquiry should include a separate duty sheet for every crane. The schedule below identifies the minimum technical information required to compare proposals on the same basis.

    Specification Group Required Information Procurement Effect
    Load and Attachment Maximum and normal payload, temperature, dimensions, centre of gravity, attachment type and attachment mass Determines capacity, reeving, trolley, headroom and pickup system
    Geometry Runway span and length, rail elevation, lift, hook approaches, bay section, obstructions and service access Defines crane envelope, girder depth, trolley arrangement and usable coverage
    Duty and Performance Hours, cycles, starts, load spectrum, production rate, travel distances, speeds, positioning and design life Controls working class, motor duty, brake duty, wheel life and lifecycle cost
    Environment and Safety Heat, dust, fumes, moisture, splash, hazardous zones, required redundancy and emergency operating philosophy Defines protection, enclosure, cooling, braking, monitoring and test scope
    Runway and Power Rail section, structural capacity, allowable reactions, power supply, earthing, feeder location and conductor scope Prevents late building reinforcement and electrical interface changes
    Commercial Boundary Standards, inspection, documentation, spares, delivery term, unloading, erection, commissioning, testing and training Creates comparable offers and exposes excluded project costs

    Representative Steel Mill and Foundry Crane Projects

    Comparable project evidence should match the process duty, handled material, capacity, attachment, environment and control philosophy. The following Henan Mine Crane projects represent three distinct steel-production requirements.

    360 ton four girder foundry crane project
    360 t four-girder, four-rail, dual-trolley crane for molten metal and heavy foundry loads.

    PROJECT 01 · HEAVY FOUNDRY

    360 t Foundry Crane

    The project uses a four-girder, four-rail, dual-trolley arrangement for a heavy casting workshop. The engineering scope addresses ultra-heavy ladle loads, thermal exposure, redundant hoisting functions and plant runway reactions.

    Review the 360 t Foundry Crane Project

    four girder casting crane for continuous steelmaking operations
    Four-girder casting crane developed for ladle transfer, pouring and heavy metallurgical service.

    PROJECT 02 · CASTING SHOP

    Four-Girder Casting Crane

    Independent main and auxiliary trolley functions support heavy molten-metal transfer and process assistance. Structural stiffness, load distribution, high-temperature protection and maintainable mechanism access form the core design requirements.

    Review the Four-Girder Casting Crane Project

    rotating electromagnetic beam crane for steel products
    Rotating electromagnetic beam crane for lifting, orienting and stacking long ferrous material.

    PROJECT 03 · FINISHED STEEL HANDLING

    Rotating Electromagnetic Beam Crane

    The rotating beam arrangement handles plate, billets, bars and other long ferrous loads without manual slinging. Magnet layout, rotation envelope, stacking orientation, anti-sway and power-loss holding are coordinated as one system.

    Review the Electromagnetic Crane Project

    Engineering, Manufacturing and Project Documentation

    A reliable steel mill crane purchase establishes the design criteria, inspection points, functional tests and handover records before manufacture. Henan Mine Crane aligns the technical document schedule with the selected product, destination requirements and contracted supply scope.

    Engineering Package

    • Design criteria and duty classification basis
    • General arrangement and hook-coverage drawings
    • Wheel loads and runway reaction schedule
    • Attachment, safety-function and control narratives

    Manufacturing Controls

    • Material identification and certificate review
    • Welding, dimensional and structural inspection
    • Mechanism, wheel, rope, brake and attachment checks
    • Heat shielding, cabin and electrical enclosure inspection

    Testing and Handover

    • Factory mechanism, brake, limit and interlock tests
    • Inspection records and component certificates
    • Site commissioning and specified load testing
    • Operation, maintenance and spare-parts documents

    Governing standards, destination regulations, third-party inspection, witness points, certificate formats, document language and acceptance responsibilities should be named in the inquiry. Compliance is confirmed for each selected crane and contracted scope.

    Delivery, Installation, Commissioning and Maintenance

    Shipment and Site Readiness

    Transport segmentation, packing, unloading route, erection equipment, runway completion, power availability, production shutdowns and work permits are coordinated before dispatch.

    Erection and Alignment

    Installation covers bridge and trolley assembly, rail and wheel interface checks, attachment installation, cabin systems, electrification and verification of process clearances.

    Commissioning and Acceptance

    Commissioning verifies motions, brakes, limits, overload functions, emergency responses, attachment controls, alarms, plant interlocks and specified no-load and load tests.

    Lifecycle Maintenance

    Maintenance plans address ropes, drums, sheaves, hooks, attachments, brakes, wheels, rails, heat shields, cabins, magnets, grabs, electrical systems and safety functions based on duty and condition.

    Steel Mill and Foundry Crane Price

    Public international equipment listings indicate approximately US$8,000–US$50,000+ for basic steel-mill double-girder, hook, grab or magnetic overhead crane configurations. Market guidance for more specialized electromagnetic process cranes commonly reaches approximately US$25,000–US$95,000+.

    New ladle and heavy foundry crane listings span approximately US$60,000 to more than US$2,000,000 per set. These figures are market-screening references, not fixed Henan Mine Crane prices. High-capacity four-girder, automated, slab, coil and complete installed systems require an engineered commercial proposal.

    Cost Package Typical Inclusions Principal Cost Drivers
    Crane Equipment Bridge, trolley, hoisting and travel mechanisms, cabin or controls, electrification and specified safety functions Capacity, span, lift, duty, speeds, redundancy, heat exposure and automation
    Attachment Package Ladle beam, gantry hook, magnet beam, grab, clamp, tong, C-hook, rotation and attachment controls Material geometry, temperature, pickup force, rotation, holding and failure response
    Runway, Building and Power Rails, runway beams, columns or reinforcement, conductor system, isolators, feeder and plant interfaces when included Runway length, reactions, existing structure, foundations, power supply and local construction rates
    Delivery and Site Services Packing, freight, unloading, erection supervision or installation, commissioning, load testing, training and inspection support Destination, shipment size, access, shutdown schedule, labor, test loads and regulatory process

    Commercial comparisons must use the same load, attachment, span, lift, duty, safety architecture, heat protection, automation, runway boundary, documentation, delivery term and site-service scope. Equipment-only listings are not directly comparable with complete installed-system quotations.

    Steel Mill and Foundry Crane FAQ

    What cranes are used in a steel mill?

    Common types include scrap and bulk-material grab cranes, charging cranes, ladle and casting cranes, slab and billet cranes, magnetic plate and bar cranes, coil-handling cranes, quenching cranes and general maintenance bridge cranes.

    What is the difference between a steel mill crane and a foundry crane?

    Steel mill crane is a broad term covering cranes throughout the production facility. A foundry crane is a specialized member of this family designed for molten-metal ladles, pouring and related high-temperature casting operations.

    Can one crane handle scrap, ladles and finished steel?

    A single crane should not be assumed suitable for all three duties. The attachments, load paths, working classes, heat exposure and required failure responses differ. Multi-purpose service requires explicit engineering and approval for every load case.

    How is foundry crane capacity calculated?

    Rated load includes molten metal, ladle shell and refractory lining, ladle beam or gantry hook, rigging and required design allowances. Liquid-metal mass by itself is not the complete suspended load.

    Which working class is required?

    Henan Mine Crane metallurgical product families are listed from A6 to A8. The final classification follows operating time, starts, load spectrum, cycle rate, process risk and the selected classification standard; rated capacity alone does not determine duty.

    How are steel mill cranes protected from heat and dust?

    Protection can include heat shields, heat-resistant cables and motors, ventilated or cooled cabinets, insulated cabins, protected brakes, dust-resistant enclosures and temperature monitoring. The package follows the measured ambient and radiant exposure.

    What happens if power is lost during magnetic lifting?

    The required response is established from the load and risk assessment. A magnetic system can include stored-energy holding, alarm, monitored power condition and a defined safe-placement procedure. Holding duration and test method must be specified.

    Can steel mill cranes operate automatically?

    Automatic task dispatch, positioning, anti-sway, collision avoidance, load tracking, inventory interfaces and remote monitoring can be integrated where the process layout, exclusion zones, communications and safety concept support automation.

    How much do steel mill and foundry cranes cost?

    Basic steel-mill crane listings commonly begin around US$8,000–US$50,000+, specialized magnetic systems can reach approximately US$25,000–US$95,000+, and listed heavy ladle and foundry equipment spans roughly US$60,000 to more than US$2,000,000 per set. Final cost requires a project specification.

    What information is required for a quotation?

    The RFQ should include process area, handled material, temperature, maximum and normal load, attachment, span, lift, runway length, operating cycle, required speeds, environment, control method, power supply, standards, inspection and delivery and installation scope.

    Request a Steel Mill and Foundry Crane Quote

    Henan Mine Crane prepares a bay-by-bay crane configuration, attachment schedule, safety scope and commercial boundary from the production and site data. The RFQ should include:

    • Process area and handled material for each crane, including temperature, dimensions and maximum and normal mass.
    • Required ladle beam, gantry hook, magnet, grab, clamp, tong, C-hook or other below-hook attachment.
    • Runway span and length, lifting height, rail elevation, building section, obstructions and allowable reactions.
    • Operating hours, cycles, load spectrum, production rate, required speeds, positioning and process interlocks.
    • Ambient and radiant heat, dust, fumes, splash exposure, indoor or outdoor service and operator-control method.
    • Power supply, project country, governing standards, inspection plan, delivery term and installation boundary.
    Henan Mine CraneDiscuss your requirements ↗
  • Steel Fabrication Crane Systems

    Steel Fabrication Crane Systems

    Steel Fabrication Crane Systems

    Henan Mine Crane · Material-Flow Systems for Steel Fabrication

    Steel Fabrication Crane Systems

    Overhead, gantry, semi-gantry and magnetic crane systems engineered for plate, beam, section, pipe, frame and welded-assembly handling from receiving through cutting, fit-up, welding, finishing and dispatch.

    Henan Mine Crane configures each steel fabrication crane from the complete load matrix, longest component, lifting attachment, required coverage, handling frequency, workstation sequence, building capacity, positioning performance, environment and applicable project standards.

    steel fabrication crane operating in an industrial production workshop
    A steel fabrication crane system is planned around the complete material route—not only the heaviest lift—from raw stock receiving to finished-assembly dispatch.

    PRIMARY LOADS

    Plate, Beam, Pipe & Frames

    CRANE OPTIONS

    Bridge, Gantry & Semi-Gantry

    LOAD-HANDLING OPTIONS

    Hooks, Beams, Clamps & Magnets

    CONTROL OPTIONS

    Pendant, Radio, Cabin & PLC

    What Is a Steel Fabrication Crane?

    A steel fabrication crane is a material-handling system configured for structural steel, platework, tanks, machinery frames, bridge components, pressure equipment, pipe assemblies and other fabricated metal products. It moves raw steel and work-in-process between stock, cutting, drilling, fit-up, welding, turning, inspection, surface treatment and shipping areas.

    The term describes an application rather than one fixed crane design. A small fabrication bay may use a single-girder overhead crane with radio control. Long welded assemblies may require two hoists or a double-trolley bridge. Raw plate handling may justify a magnetic beam. An outdoor stockyard may need a gantry crane, while a side bay or machine station may be served by a semi-gantry crane.

    Steel fabrication is also different from primary steelmaking. Most fabrication shops handle solid material at ambient temperature, while foundry and metallurgical cranes address molten metal, extreme heat and a different safety architecture. Henan Mine Crane selects the system from the actual fabrication process using its single-girder bridge crane, double-girder bridge crane, semi-gantry crane and gantry crane platforms.

    Steel Fabrication Applications by Process Area

    Receiving and Raw Stock

    Unload and store plate, H-beams, I-sections, angles, pipes and bars with hooks, approved clamps, spreader beams or magnetic systems matched to the material.

    Cutting and Preparation

    Feed plasma, laser, oxy-fuel, saw, drill and edge-preparation stations while controlling plate orientation, table approach and clearance above machinery.

    Fit-Up and Welding

    Position beams, shells, stiffeners, frames and subassemblies at jigs, rotators and welding stations using creep speed and clear operator sight lines.

    Turning and Repositioning

    Rotate or tail long fabrications only through a documented lifting method using two hooks, two cranes, a turning beam or purpose-designed fixtures.

    Blasting, Painting and Finishing

    Transfer finished steel through cleaning, coating, curing and inspection zones with environmental protection selected for dust, moisture, paint and solvent conditions.

    Assembly and Dispatch

    Support trial assembly, dimensional inspection, weighing, staging and truck loading for structural frames, vessels, modules and completed equipment.

    overhead crane supporting steel fabrication workshop material flow
    Crane coverage should follow the production route and eliminate repeated floor handling between stock, fabrication, inspection and dispatch positions.

    System Components and Operating Principle

    1. Bridge, gantry or semi-gantry structure: provides the required work area while transferring vertical, transverse, longitudinal and dynamic loads to the building or ground-supported runway.
    2. Hoist or process trolley: supplies the capacity, lift, speed, reeving, brakes and duty required for the declared fabrication cycle.
    3. End carriages and drives: move the crane along the runway with speed control, alignment, braking and wheel loads matched to the structure.
    4. Below-hook equipment: connects hooks to plate, sections, pipe or assemblies through approved slings, beams, clamps, magnets or custom fixtures.
    5. Power and controls: coordinate lifting and travel through pendant, radio, cabin or PLC-assisted operation, including limits, overload monitoring and optional anti-sway.
    6. Runway and electrification: include rails, beams, columns or brackets, conductor system, isolators, access and maintenance provisions where specified.
    electric hoist bridge crane machinery for steel fabrication handling
    Bridge structure, mechanisms, attachment, runway, controls and installation interfaces form one material-handling system.

    Rated-load basis: capacity starts with the maximum gross suspended load. Include the steel component, spreader beam, lifting magnet, clamps, slings, shackles, hook block and every suspended accessory. Also define eccentric loads, multiple pickup points, retained blasting media or liquid and approved turning cases.

    Steel Fabrication Crane Selection Considerations

    Selection begins with the complete material-flow map. The heaviest load establishes only part of the requirement; long-load stability, workstation access, cycle frequency and the building interface frequently determine the final configuration.

    Load Matrix

    Raw plate and sections, work-in-process and finished assemblies; minimum, normal and maximum mass; dimensions; center of gravity; stiffness; pickup points and attachment mass.

    Material Route

    Receiving, stock, cutting, drilling, fit-up, welding, inspection, blasting, coating and dispatch locations; required transfers, crossings, buffers and future expansion.

    Duty and Cycle

    Lifts per hour, starts, travel distance, shifts, annual hours, load spectrum, simultaneous motions, peak production, maintenance window and consequence of downtime.

    Long-Load Control

    Maximum component length, permissible deflection, hook spacing, two-hoist or two-crane operation, synchronization, load sharing, permitted rotation and tag-line method.

    Building and Runway

    Rail-center span, runway length and elevation, headroom, hook approaches, column spacing, wheel-load limits, clearances, foundations and installation access.

    Attachment and Surface

    Hook, slings, beam, clamp, magnet or vacuum device; material grade, surface condition, temperature, edge geometry, coating and acceptable contact marks.

    Environment

    Indoor or outdoor use, ambient range, welding fume, grinding dust, blasting media, humidity, paint or solvent area, wind, corrosion and wash-down requirements.

    Control and Acceptance

    Pendant, radio, cabin or automation; creep speed; anti-sway; restricted zones; collision avoidance; proof load; representative-load trial and documentation.

    Steel Fabrication Crane Configurations Compared

    The comparison separates crane structures and handling functions that can serve the same plant but are not interchangeable.

    Configuration Typical Fabrication Duty Main Advantage Primary Limitation Selection Trigger
    Single-Girder Overhead Crane General stock, parts and assembly handling Lower self-weight and compact system Capacity, span, headroom and service intensity must remain within the selected platform Light-to-medium loads with one principal pickup point
    Double-Girder Overhead Crane Heavy frames, machinery structures and intensive production Higher capacity and flexible trolley arrangements Greater self-weight and runway reaction Heavy loads, wide span, high duty or demanding approaches
    Double-Trolley Overhead Crane Long beams, vessels, frames and controlled turning Two lifting points can operate independently or in an approved synchronized mode Load sharing and synchronization require defined controls and procedures Long, flexible or offset assemblies need two-point support
    Electromagnetic Crane Ferromagnetic plate, sections, billets and steel offcuts Fast pickup without manual sling placement Material, surface, thickness, air gaps and power-loss retention must be validated Repetitive handling of compatible magnetic material
    Semi-Gantry Crane Side bay, machine line or local production area One elevated rail and one floor rail reduce the need for a full runway on both sides Floor rail affects aisle planning and guarding Only one suitable building runway side is available
    Gantry Crane Outdoor steel stock, large fabrications and loading area Ground-supported coverage independent of the workshop roof Ground rails, foundations, weather, wind and vehicle crossings require coordination Outdoor or open-yard material flow
    double-girder crane selected for heavy steel fabrication work
    The lowest-cost crane structure is not always the lowest-cost production solution. Coverage, duty, attachment, runway and cycle time must be compared on one operating basis.

    Published Configuration Reference Ranges

    The ranges below summarize published Henan Mine Crane product platforms that can be configured for steel fabrication. They are preliminary selection references rather than one universal steel fabrication crane model.

    Product Platform Published Capacity Published Span Published Lift Published Class Typical Fabrication Role
    European-Style Single Girder 1–10 t 7.5–28.5 m 6–30 m A3–A5 General workshop handling
    Electric-Hoist Double Girder 3–32 t Up to 31.5 m in the published base range Project-specific A3–A6 Heavier or more intensive production
    Double-Trolley Electric Hoist Crane 1+1 to 32+32 t 7.5–31.5 m 6–30 m A5–A6 Long loads and two-point lifting
    Electromagnetic Bridge Crane 5–32 t including magnet weight 10.5–31.5 m 6–30 m A1–A8 published; select by duty Plate and ferromagnetic stock transfer
    Single-Girder Semi-Gantry 1–32 t 6–35 m 4–20 m A3–A5 Local side bay or machine line
    European Single-Girder Gantry 1–32 t 6–35 m 4–20 m A3–A5 Outdoor stock and dispatch yard
    Specification control: final capacity, span, lift, speed, classification, wheel loads, attachment and environmental protection are confirmed from the approved duty. The signed technical agreement and general arrangement govern the supplied system.

    Long Loads, Two-Point Lifting and Turning

    Long beams, trusses, shells, pipes and welded frames may be lighter than the crane capacity but still govern the design. The lift plan must control bending, torsion, pickup spacing, local contact stress, center-of-gravity uncertainty and the effect of unequal hoist motion.

    • One hoist with spreader: suitable when the beam or fixture distributes the load and the center of gravity remains within the approved range.
    • Two hoists on one crane: supports adjustable hook spacing and controlled load sharing for long components.
    • Two independent trolleys: offers broader spacing and separate operation, with synchronization only when engineered and permitted.
    • Two-crane tandem lift: requires defined command control, compatible speeds, capacity allocation, communication and a site lifting plan.
    • Turning operation: requires a documented sequence, approved attachments, controlled load path and adequate clear space; it is not created by capacity alone.
    double-trolley overhead crane for long steel fabrication assemblies
    Two lifting points can improve support for long assemblies, but the quotation must define hook spacing, capacity split, synchronization and permitted operating modes.

    Tandem-load data: provide the heaviest and longest component drawings, lifting-point coordinates, center-of-gravity tolerance, permissible deflection, required rotation, minimum and maximum hook spacing and the allowable difference between lifting points.

    Lifting Attachments for Plate, Sections and Assemblies

    Attachment Suitable Load Data Required Critical Limitation
    Hook with Slings General frames, machinery and approved lifting points Sling angle, edge protection, headroom, pickup points and load balance Manual rigging time and safe access
    Spreader or Lifting Beam Long beams, pipes, trusses and flexible assemblies Pickup spacing, adjustment range, load cases, beam mass and storage Attachment mass consumes crane capacity and headroom
    Plate or Beam Clamp Compatible plate edges, flanges and profiles Thickness, hardness, surface, orientation, jaw range and approved use Wrong geometry or side loading can invalidate the clamp rating
    Electromagnet or Magnetic Beam Ferromagnetic plate, sections and offcuts Material, thickness, flatness, temperature, surface, air gap, load layers and retained-load strategy Not every steel grade, shape or surface condition is suitable
    Vacuum Lifter Compatible smooth plate where surface contact is acceptable Surface porosity, condition, temperature, plate size and backup provisions Scale, rust, holes or rough surfaces can prevent reliable sealing
    Custom Fixture or Turner Repeated product families and controlled rotation All product variants, engagement, fail-safe behavior, changeover and test method Requires product-specific design and acceptance
    electromagnetic bridge crane for handling steel plate and sections
    Magnetic handling can reduce manual rigging, but load compatibility and the safe response to power loss must be verified for every approved material family.

    Attachment Capacity Is Part of Crane Capacity

    A 10 t workpiece with a 2 t beam and rigging requires more than a 10 t crane. The same principle applies to magnets: the published crane rating may include the magnet mass, so usable material capacity must be confirmed explicitly.

    Attachment storage, changeover, electrical connections, identification, inspection status and the prevention of wrong-device selection should be included in the operating concept.

    Workshop Layout, Runway and Production Coverage

    A fabrication-crane quotation should show the useful hook envelope, not only the nominal span. Columns, end approaches, trolley approach, hook block size, roof bracing, lighting, extraction ducts, machines and maintenance platforms can create blind areas.

    New Workshop

    Coordinate crane wheel loads, rail elevation, column grid, roof clearance, maintenance access and electrification before structural steelwork is released for fabrication.

    Existing Runway

    Survey rails, beams, brackets, columns, connections and foundations for geometry, wear, corrosion, fatigue and the reactions from the proposed crane and duty.

    Outdoor Yard

    Define foundations, rail drainage, vehicle crossings, stormwater, wind operating limits, storm securing, corrosion category, temperature and safe parking position.

    gantry crane for outdoor structural steel fabrication stockyard
    A gantry crane can connect outdoor stock and dispatch areas without loading the workshop roof, provided foundations, rails, weather and traffic interfaces are included.

    Controls, Positioning and Workshop Environment

    Control Strategy

    Radio control commonly supports mobile fabrication teams and a direct view of the load. Pendant control can suit local, lower-speed work. A cabin may be justified for heavy, repetitive or long-travel service. PLC-assisted functions can add stored positions, restricted zones, anti-sway, collision avoidance, diagnostics and production-system interfaces.

    Required positioning should be stated as a measurable tolerance at a defined load, speed and location. Creep speed, brake response, load swing and operator visibility are often more important at a welding jig than maximum travel speed.

    Environmental Review

    Welding fumes, conductive grinding dust, blasting media, humidity and outdoor corrosion influence motor, brake, cable, bearing, enclosure, coating and maintenance decisions. A paint or solvent area requires a documented hazardous-area review before electrical equipment is selected.

    An explosion-protected crane is not selected solely because painting occurs somewhere in the plant. The owner’s area-classification documents, substance data, ventilation and local rules establish whether special electrical protection is required.

    custom double-girder overhead crane for heavy fabrication and assembly
    Heavy-load capability, precise low-speed control and production availability are selected together from the declared fabrication duty.

    Design Basis, Inspection and Acceptance

    The contract identifies the destination, governing crane classification, structural and mechanism rules, electrical requirements, below-hook device standard, local inspection and registration route. Depending on the project, the design basis may reference ISO 4301 classification; EN 13001, EN 15011 and EN 13155; or CMAA 70 with applicable ASME B30.2, B30.20 and BTH-1 provisions. Local law and the signed specification govern final compliance.

    Design Review

    Load and duty matrix, classification, fatigue basis, deflection criteria, wheel loads, attachment, control philosophy, environmental data, access and interface schedule.

    Factory Inspection

    Material traceability, welding and NDT records as specified, dimensions, mechanism tests, panels, software, limits, alarms, coating and document review.

    Site Acceptance

    Runway and alignment checks, functional and load tests, attachment trial, long-load sequence, controls, safety functions, training, spares and final documentation.

    Representative-load test: where practical, acceptance should include the longest or most difficult approved fabrication, the intended attachment, actual pickup points, normal operators and the required workstation approach—not only a compact test weight.

    Published Industrial Manufacturing References

    intelligent crane supplied for heavy equipment structural production

    XCMG Manufacturing Program

    A published Henan Mine Crane industrial-manufacturing reference states that more than 300 intelligent cranes of multiple types were contracted for XCMG Group and used across construction-machinery assembly and structural production processes.

    View the Published Industrial Manufacturing Reference →

    double-girder crane serving a tall heavy fabrication workshop

    Tangxing Heavy Equipment Plant

    A separate published reference reports more than 100 cranes for a trenchless-equipment industrial park, configured for a 25 m-high heavy steel plant and production supporting an annual output of 500 pipe-jacking machines.

    View the Published Smart Factory Reference →

    Evidence boundary: these references demonstrate batch crane supply for structural production, assembly and heavy equipment manufacturing. They do not establish one standard steel fabrication crane specification; every new system is configured from its own loads, layout, duty and acceptance criteria.

    Steel Fabrication Crane Price and Budget Scope

    Steel fabrication crane prices vary materially because public listings may describe only a basic crane package or kit, while an operational project can also require bridge girders, runways, electrification, attachments, freight, erection, commissioning and local inspection.

    A public market review completed on 20 September 2026 found an ordinary 1–10 t single-girder overhead crane listing at US$2,600–5,500 per set. A separate United States listing showed US$28,500 for a 10 t top-running single-girder crane kit, explicitly excluding bridge beams, runway rails, runway conductor bar, fabrication and installation. These figures are scope examples, not Henan Mine Crane quotations and not complete installed steel-fabrication systems.

    Public Reference Published Price Scope Interpretation Budget Use
    Ordinary 1–10 t Single-Girder Listing US$2,600–5,500 per set Marketplace FOB reference with limited project boundary Indicative equipment listing only
    10 t Top-Running Single-Girder Crane Kit US$28,500 Kit only; bridge beams, runways, runway electrification, fabrication and installation excluded Useful example of component-scope pricing
    Complete Steel Fabrication Crane Project Project quotation Crane, runway, attachment, interfaces, logistics and site services as specified Required for a comparable procurement budget

    Main Cost Drivers

    Crane Structure
    Capacity, span, lift, single or double girder, one or two trolleys and working classification.
    Runway and Building
    Rails, beams, columns, foundations, wheel loads, access platforms and structural modification.
    Attachment
    Spreader, clamps, magnets, custom fixtures, electrical supply, storage and proof testing.
    Controls
    VFD motion, radio, cabin, synchronization, anti-sway, collision avoidance and automation.
    Environment
    Dust protection, hazardous-area equipment, corrosion system, outdoor wind and temperature.
    Project Scope
    Freight, duties, erection, electrification, commissioning, testing, training, spares and documentation.

    Comparable quotation rule: issue the same load matrix, material-flow plan, duty, building data, attachment requirement, standards and supply boundary to every supplier. Require a priced list of inclusions, exclusions, provisional items, utilities, site services and acceptance tests.

    Information Required for a Steel Fabrication Crane Quote

    A complete enquiry allows the crane, runway, attachment, controls and site services to be selected and priced on one defined basis.

    Load and Attachment Data

    Maximum gross load, normal load distribution, dimensions, center of gravity, material and surface, pickup points, lifting beam, clamps, magnets, slings and finished-product drawings.

    Production Duty

    Process map, lifts and starts per hour, shifts, annual hours, load spectrum, travel distance, simultaneous motion, cycle target, availability and future capacity plan.

    Workshop and Runway

    Rail-center span, runway length and elevation, lift, headroom, approaches, column spacing, rail and beam details, existing wheel-load limits, foundations and installation access.

    Long-Load Operations

    Maximum length, stiffness, hook spacing, two-point load sharing, synchronization tolerance, turning sequence, tandem operation and clearance envelope.

    Controls and Environment

    Pendant, radio, cabin or automatic mode; speed and positioning; anti-sway; collision zones; power supply; dust, fumes, paint area, humidity, corrosion, temperature and outdoor wind.

    Commercial and Compliance Scope

    Destination, standards, inspection route, Incoterm, freight, runway, installation, electrification, commissioning, load test, operator training, spares, documentation and warranty.

    Fastest route to a comparable proposal: provide a workshop cross-section, equipment layout, material-flow arrows, load and attachment matrix, longest-product drawing and required supply boundary. Unknown items can be identified as open points instead of being hidden in a lump-sum price.

    Frequently Asked Questions

    Which crane is suitable for a steel fabrication shop?

    Single-girder cranes commonly serve light-to-medium general handling. Double-girder cranes suit heavier or more intensive duty. Long loads may require two hoists or trolleys, while outdoor stock normally favors a gantry crane.

    How is crane capacity calculated?

    Add the heaviest workpiece, beam, magnet, clamps, slings, shackles, hook block and every suspended component. Then evaluate eccentric loading, multiple pickup points, load sharing, dynamics and approved turning cases.

    When are two hoists or two trolleys required?

    They are considered when a long or flexible assembly needs two support points, when hook spacing must change, or when an approved turning sequence requires separate control. Capacity split and synchronization must be specified.

    Can an electromagnetic crane lift every steel plate?

    No. Magnetic properties, thickness, flatness, temperature, coating, rust, scale, air gaps and stacked layers affect holding performance. The magnet and power-loss strategy must be validated against each approved load family.

    How much does a steel fabrication crane cost?

    Public equipment references reviewed in September 2026 ranged from US$2,600–5,500 for one ordinary 1–10 t single-girder listing to US$28,500 for a 10 t crane kit. Neither represents a complete installed project; final price depends on the full technical and commercial scope.

    Can an existing runway be reused?

    Only after rails, beams, brackets, columns, connections and foundations are checked for condition, geometry, fatigue and the proposed vertical, horizontal and dynamic crane reactions.

    Is radio control suitable for fabrication?

    Radio control can provide a direct view of the load and mobility between workstations. The risk assessment must still define operator position, emergency stop coverage, travel warnings, restricted zones and control of multiple cranes.

    What should be tested before handover?

    Testing covers motions, brakes, limits, overload protection, controls, attachments, positioning, collision functions, representative long loads, tandem modes, proof load and the agreed emergency response.

    Request a Steel Fabrication Crane Quote

    Submit the load and attachment matrix, longest-product drawing, production flow, lifts per hour, span, lift, runway and building data, control requirements, environment, destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.

    Henan Mine CraneDiscuss your requirements ↗
  • Slab Handling Crane for Steel Mill Storage and Transfer

    Slab Handling Crane for Steel Mill Storage and Transfer

    Slab Handling Crane for Steel Mill Storage and Transfer

    Henan Mine Crane · Steel Mill Process Cranes

    Slab Handling Crane for Steel Mill Storage and Transfer

    A heavy-duty overhead crane engineered for lifting, transporting, turning, stacking and dispatching hot or ambient steel slabs across continuous-casting, cooling, conditioning, warehouse and rolling-mill interfaces.

    Henan Mine Crane configures YB slab handling cranes with clamps, magnetic beams, synchronized lifting, slewing systems, PLC control and optional automation. Final design follows slab geometry, gross suspended mass, temperature exposure, handling route, duty and plant interfaces.

    Henan Mine Crane slab handling crane for steel mill transfer and stacking
    Crane structure, lifting attachment, thermal protection and control logic are engineered as one process-handling system.

    HANDLED MATERIAL

    Hot & Ambient Steel Slabs

    ATTACHMENT OPTIONS

    Clamp, Magnet or Beam

    SERVICE PROFILE

    A7–A8 Published Range

    CONTROL OPTIONS

    Cabin, PLC & Automation

    What Is a Slab Handling Crane?

    A slab handling crane is a purpose-engineered metallurgical overhead crane that moves semi-finished steel slabs between production and storage stages. Typical duties include receiving slabs from a continuous caster, clearing a cooling bed, transferring material to inspection or scarfing stations, organizing stockyard stacks, feeding a reheating furnace and loading railcars, trucks or internal transfer equipment.

    The equipment differs from a general hook crane because the slab itself defines the lifting system. Length, width, thickness, surface temperature, camber, scale condition, stack spacing and permitted contact zones determine whether a mechanical clamp, electromagnetic beam, hook beam or another approved attachment can establish secure load control. High cycle frequency and precise placement may also require synchronized lifting, anti-sway, low-speed positioning, coordinate control and production-system communication.

    Rated capacity cannot be selected from slab net weight alone. The engineering basis must identify whether the contractual capacity represents slab payload or gross suspended load. A complete gross-load calculation includes the maximum slab or slab group, clamp or magnet beam, rotating structure, hook blocks, equalizing equipment and every component suspended below the trolley. Dynamic factors and the governing design basis are then applied.

    Henan Mine Crane configures YB slab cranes for hot and ambient handling. Final project drawings define attachment geometry, control logic, safety functions and inspection requirements.

    Slab Handling Crane Configurations

    01 · Mechanical Slab Clamp Crane

    Side-gripping mechanical or powered tongs engage approved slab faces. The arrangement avoids dependence on magnetic holding power and suits defined thickness and width ranges. Jaw geometry, closing force, locking status, surface scale and anti-release protection require project approval.

    02 · Electromagnetic Slab Crane

    A suspended magnet beam lifts magnetically responsive slabs without side access. Fast pickup and release support high-throughput yards, but magnetic duty, slab temperature, air gaps, power continuity, residual magnetism and emergency retention strategy govern suitability.

    03 · Fixed-Orientation Transfer Crane

    A non-slewing lifting system transfers slabs along a consistent storage or production axis. Reduced rotating mass and simpler control can support dependable repetitive handling when pickup and placement orientations remain aligned.

    04 · Rotating Slab Handling Crane

    A slewing trolley or rotating beam changes slab orientation between process bays, stacks, inspection lines and dispatch lanes. Rotation envelope, cable management, load inertia, collision zones and positioning accuracy form part of the crane design.

    05 · Automated Slab Warehouse Crane

    PLC control, encoders, ranging devices, anti-sway, stack coordinates and plant communication support unmanned or supervised automatic cycles. Manual recovery, safe-zone logic, inventory reconciliation and degraded-mode operation remain essential.

    06 · Synchronized Dual-Lift System

    Two lifting points or a 50+50 t arrangement distribute load along long slabs and specialized clamps. Load sharing, hoist synchronization, skew monitoring, rope reeving and independent protective functions limit twist and unequal loading.

    Compare Slab Lifting and Motion Configurations

    Configuration Load Interface Principal Advantage Engineering Constraint Typical Application
    Mechanical slab clamp Side faces or defined gripping zones No magnetic holding dependency; positive mechanical interface Requires approved thickness, width, edge condition and jaw access; contact marks may require review Hot or ambient slabs with stable geometry and controlled stack gaps
    Electromagnetic beam Upper slab surface through magnetic attraction Fast pickup; no side access; adaptable magnet grouping Ferromagnetic material only; air gap, temperature, scale, power loss and residual magnetism affect performance Ambient or temperature-approved slabs in repetitive storage and dispatch
    Hook or lifting beam Engineered lifting points, chains or approved rigging Flexible for unusual pieces and maintenance loads Slower cycle; manual rigging exposure; lifting points and sling angles require control Low-frequency handling or slabs with dedicated lifting interfaces
    Non-slewing trolley Clamp, magnet or beam kept on fixed axis Simpler operating path and lower rotating complexity Cannot correct orientation without another handling stage Straight transfer between aligned production and storage points
    Slewing trolley or beam Attachment rotates around a controlled vertical axis Places slabs across different bay and stack orientations Higher dead load, headroom demand, inertia and collision-control complexity Warehouses, conditioning lines and multi-direction dispatch layouts
    Automatic coordinate handling Attachment combined with sensors and stored positions Repeatable stacking, traceable moves and reduced cycle variation Requires reliable slab identity, clear zones, recovery logic and maintained calibration High-throughput finished-slab warehouses and integrated production systems

    Attachment selection rule: slab temperature, magnetic properties, dimensional range, surface condition, stack access and failure consequence must be established before crane capacity, trolley layout and control functions are frozen.

    Slab Handling Applications Across the Steel Process

    Process Area Material Condition Primary Handling Demand Configuration Direction Data Required for Engineering
    Continuous-casting discharge Newly cast hot slabs leaving the caster or transfer table High radiant heat, production continuity and controlled pickup Heat-shielded clamp crane with precise low-speed approach Slab temperature, caster rhythm, transfer path and standby strategy
    Cooling bed and slab yard Hot slabs during staged cooling and buffer storage Changing temperature, stack sequence and large coverage area Clamp or approved magnetic system with coordinated yard travel Cooling layout, dwell time, stack geometry and exclusion zones
    Inspection and conditioning Slabs routed to grinding, scarfing, marking or flaw detection Accurate presentation and possible orientation change Rotating clamp, magnet beam or engineered lifting beam Required angle, placement tolerance and process-station interface
    Finished-slab warehouse Ambient slabs stored by grade, heat, order or destination Inventory accuracy, dense stacking and repetitive cycles Automated or semi-automated crane with coordinate control Warehouse map, stack rules, identification method and throughput
    Reheating-furnace feed Selected slabs transferred from storage to rolling preparation Production sequencing and furnace charging interface High-duty crane with controlled placement and plant interlocks Furnace schedule, buffer capacity, transfer equipment and cycle time
    Rail, truck or internal dispatch Slabs loaded to transport equipment or transfer cars Vehicle position variation and personnel separation Clamp, magnet or lifting beam with zone monitoring Deck geometry, securing plan, loading sequence and access controls

    A hot-slab transfer crane may prioritize thermal protection, heavy duty and availability; an ambient warehouse crane may prioritize inventory control, positioning and dense storage. Materially different process conditions can require separate operating modes or separate cranes.

    Slab Handling Crane Technical Selection Framework

    The following range reflects the published Henan Mine Crane YB product envelope and a practical quotation framework. It is not a universal rating for every slab, building or destination. Final values appear on the approved project data sheet and general arrangement.

    Selection Item Preliminary Engineering Envelope Project Data Required Procurement Control
    Rated lifting capacity 20–150 t published configurable range; 50+50 t documented project arrangement Maximum slab mass, number of slabs, attachment mass and contractual capacity definition Confirm net payload versus gross suspended load before mechanism sizing
    Span 10–39 m published configurable range Runway rail-center distance, working coverage, end approaches and building reactions Building clear width is not substituted for crane span
    Lifting height 5–23 m published configurable range Lowest pickup, highest stack, attachment depth, rail elevation and service clearance Available hook or clamp elevation is checked on a vertical section
    Slab geometry Project-specific; published clamp information identifies slabs from 150 mm thickness Minimum and maximum length, width, thickness, camber, edge profile and weight distribution Every attachment operating envelope is approved in writing
    Temperature exposure Published product information identifies operation around slabs up to 650°C Slab surface temperature, ambient air, radiant exposure, distance, dwell time and heat cycles Temperature terms are separated; a slab rating is not treated as ambient-air temperature
    Duty classification A7–A8 published range, subject to governing project classification Lifts per hour, load spectrum, shifts, annual hours, travel distance and service-life target Capacity and fatigue duty are evaluated independently
    Motion performance Hoist 1–8 m/min and crane travel 10–30 m/min published ranges; other values engineered Cycle target, safe high-speed route, low-speed placement, rotation and positioning tolerance Speed follows process flow, load stability and stopping distance
    Control and power PLC/HMI options; configurable voltage and frequency; cabin, supervised or automatic operation Plant power, communication protocol, operating station, backup mode and cybersecurity boundary I/O, interlocks, data ownership and recovery sequence are documented
    Environment and protection Metallurgical heat, dust and scale; IP55 listed as a published option Temperature zones, dust, fumes, humidity, corrosion, vibration and maintenance access Enclosures, cooling, cables, lubrication and materials match the actual zone
    Runway and acceptance Project-specific wheel loads, horizontal forces, rail and test requirements Runway drawings, rail condition, destination rules, inspection authority and load-test plan Crane, building and statutory responsibilities are contractually assigned

    Safety and Control Architecture for Slab Handling

    The safety concept covers secure pickup, hoisting, travel, rotation, placement and release under the governing design basis and plant risk assessment.

    Clamp Status and Release Interlocks

    Open, closed and locked states are monitored where applicable. Hoisting permission, load presence and release conditions are interlocked so that a clamp cannot be opened during an unsafe suspended state.

    Magnet Power-Loss Strategy

    Magnetic systems require a documented response to supply interruption. Battery or alternate power, holding-time monitoring, alarms, controlled lowering and restricted personnel zones are selected from the load risk.

    Hoist and Load Protection

    Overload limitation, dual-point synchronization, upper and lower limits, brake monitoring, rope guidance and low-speed positioning protect the lifting path and prevent unequal loading.

    Anti-Sway and Position Control

    Mechanical reeving, VFD motion profiles, encoder feedback and optional electronic anti-sway reduce pendulation. Position tolerance is specified at the attachment and verified through commissioning.

    Travel, Rotation and Collision Zones

    End limits, buffers, anti-collision, slewing limits, clearance monitoring and protected storage coordinates prevent contact with structures, equipment, adjacent cranes and slab stacks.

    High-Temperature Protection

    Heat shields, protected electrical cabinets, temperature-rated cables, appropriate lubrication and component placement reduce radiant exposure. Inspection intervals reflect scale, heat and thermal cycling.

    Automated-Mode Safeguards

    Access control, zone scanning, permissive logic, fault diagnosis, safe stop, controlled restart and manual recovery govern unmanned or supervised cycles.

    Operator and Maintenance Safety

    High-visibility cabin design, cameras, warning devices, isolation points, platforms, access routes and component-removal space support controlled operation and maintainability.

    Crane Structure, Headroom and Operating Logic

    Heavy slab service commonly uses a top-running double-girder bridge with an engineered winch trolley. The arrangement provides structural stiffness, mechanism access and space for synchronized hoists, a rotating platform or a suspended clamp beam. Long slabs may require two lifting points so that load sharing and slab deflection remain controlled throughout acceleration, travel and placement.

    Headroom is governed by more than hook height. Rail elevation, bridge depth, trolley structure, rope geometry, clamp opening height, slab thickness, required clearance above stacks and maintenance-removal paths must be shown on one dimensioned vertical section. A rotating attachment also requires a verified plan-view envelope at every operating elevation.

    An automatic cycle normally includes destination validation, approach at controlled speed, attachment alignment, secure pickup confirmation, vertical clearance, bridge and trolley travel, optional rotation, stack-position verification, controlled lowering and release confirmation. Fault recovery must define retained load condition, safe manual access and the route back to a known coordinate.

    Stack height, cooling separation, grade segregation, retrieval sequence and buffer locations determine travel distance and cycle time. Motion values should follow the process model rather than maximum speed alone.

    high temperature slab stacking crane with engineered lifting attachment
    Double-girder structure, attachment geometry, heat exposure and stack clearance are coordinated in the project layout.

    Project Case: 50+50 t Slab Clamping Crane

    50 plus 50 tonne slab clamping crane manufactured by Henan Mine Crane
    Documented steel-mill project combining dual lifting capacity, electric clamp adjustment, high-temperature adaptation and intelligent monitoring.

    Henan Mine Crane manufactured a 50+50 t slab clamping crane for the Rizhao high-quality products base of Shanshan Iron & Steel. The project applies an electrically adjustable slab clamp with positioning control to large-tonnage steel-mill material handling.

    The documented configuration addresses high-temperature radiation stated above 650°C through heat-resistant structural and protective measures. Digital speed control and a guiding arrangement support stable heavy-load motion and accurate placement. PLC control, weighing, fault alarms and operating-data functions provide a foundation for monitored production and later automation integration.

    The case demonstrates that dual-point load control, clamp adjustment, thermal protection, positioning, monitoring and maintenance access must operate as one system. Temperature and performance values remain project-specific.

    View Project Case →

    Engineering, Manufacturing and Quality Documentation

    A slab handling crane should be released through an agreed document and inspection plan. Records connect the approved load case and control philosophy to the fabricated structure, assembled mechanisms and commissioned attachment.

    automated crane girder welding workstation at Henan Mine Crane
    Controlled drawings, qualified welding, dimensional inspection and functional testing support traceable project delivery.

    Approved Design Package

    General arrangement, wheel loads, attachment drawing, lifting-point geometry, mechanism data, electrical demand and control narrative.

    Structural Quality

    Material identification, approved welding procedures, welder qualification, dimensional checks and specified non-destructive examination.

    Mechanism Verification

    Hoist synchronization, brakes, drums, ropes, wheels, reducers, lubrication, rotation drives and maintenance-access checks.

    Attachment Inspection

    Clamp opening range, jaw contact, pins, locks, sensors, magnet circuits, beam geometry and safe-release interlocks.

    Functional Testing

    Motion tests, limits, alarms, overload functions, position feedback, automated sequences and contracted witness points.

    Final Handover

    Final drawings, manuals, configured parameters, inspection records, spare-parts schedule and commissioning documentation.

    Installation, Commissioning and Lifecycle Planning

    Site and Runway Verification

    Confirm rail centers, elevation, alignment, supporting structure, maximum wheel loads, horizontal forces, conductor location, erection access and available assembly space before shipment.

    Shipping and Erection Plan

    Define transport divisions, lifting points, temporary supports, girder assembly, trolley placement, attachment installation, high-temperature protection and site responsibility matrix.

    Cold Commissioning

    Verify travel alignment, brakes, limits, encoders, clamp or magnet functions, rotation, alarms, interlocks, communication and manual recovery without a process load.

    Load and Process Acceptance

    Conduct contracted static, dynamic and functional tests, then validate pickup, transfer, positioning and release using approved trial slabs and controlled operating zones.

    Attachment Maintenance

    Inspect clamp jaws, pins, bushes, locks, guides and sensors; check magnet insulation, cables, power backup and beam condition. Wear limits and replacement criteria belong in the manual.

    Thermal and Electrical Inspection

    Monitor heat shields, cable protection, cabinet cooling, seals, lubrication condition, brakes, ropes and temperature-affected components at intervals derived from actual exposure.

    Automation Support

    Maintain coordinate calibration, sensor health, network interfaces, backups, fault logs and recovery procedures. Software changes require controlled authorization and documented validation.

    Critical Spare Parts

    Plan brakes, encoders, sensors, contactors, VFD-related components, limits, seals, clamp wear parts, cable assemblies and selected magnet-power components around production consequence.

    Slab Handling Crane Price and Project Cost

    Custom slab cranes require project quotation because capacity, attachment, temperature, duty and automation change the system materially. General bridge-crane figures provide only a lower-level market benchmark; they do not represent a fixed Henan Mine Crane slab-crane price.

    Budget Level Indicative Market Position Typical Scope Main Cost Drivers Commercial Control
    General 5 t double-girder bridge benchmark Around US$60,000 in a current North American installed example Conventional bridge, trolley or hoist and installation under stated conditions Span, lift, duty, runway, regional labor and controls Not a slab-crane quotation; used only as a general-market floor comparison
    General 10 t double-girder bridge benchmark Around US$100,000 in a current North American installed example Conventional double-girder system under stated conditions Capacity, span, headroom, runway, installation and testing Not comparable with 20–150 t metallurgical process equipment
    Manual slab clamp process crane Project quotation Double-girder crane, open-winch trolley, engineered clamp and metallurgical protection Gross load, slab range, clamp adjustment, heat, duty, span and documentation Price schedule separates crane, attachment, electrification, freight and site services
    50+50 t or synchronized dual-lift crane Project quotation Dual lifting points, load sharing, high-capacity attachment and advanced monitoring Synchronization, rope system, structure, brakes, clamp, thermal protection and testing Approved load cases and supply boundary precede commercial comparison
    Automated slab warehouse crane Project quotation Crane, attachment, sensors, anti-sway, positioning, PLC and plant interface Coordinate accuracy, throughput, redundancy, system integration and recovery mode Automation hardware, software, commissioning and production trials are itemized
    Turnkey slab-handling installation Project quotation Equipment plus selected runway, delivery, erection, commissioning, load testing and training Destination, civil and runway work, access, local labor, permits and shutdown plan Equipment-only and installed-project totals remain clearly separated

    Price comparison basis: normalize capacity definition, attachment, duty, temperature protection, rotation, automation, runway, electrification, packing, freight, erection, commissioning, load testing, training and spare parts. A low equipment figure can exclude the highest-risk project interfaces.

    Information Required for a Slab Handling Crane Quote

    A complete request establishes attachment geometry, crane duty and project boundary. Slab schedules, building drawings and process-flow diagrams should accompany the following data.

    Slab Size and Mass Range

    Minimum and maximum length, width, thickness, unit mass, number lifted per cycle, camber, edge condition and center-of-gravity variation.

    Temperature and Surface Condition

    Maximum slab surface temperature, ambient temperature, radiant exposure, scale, moisture, contact restrictions and cooling pattern.

    Handling Route and Stack Plan

    Pickup and placement coordinates, transfer distance, stack orientation, maximum stack height, gaps, retrieval logic and vehicle interfaces.

    Capacity and Attachment

    Required payload, proposed clamp or magnet, attachment mass, opening range, rotation requirement, auxiliary hook and special handling modes.

    Duty and Throughput

    Moves per hour, load spectrum, shifts, annual hours, target cycle time, production criticality and standby or redundancy requirements.

    Building and Runway

    Rail centers, bridge travel, rail elevation, runway beam and rail data, column spacing, roof obstructions, wheel-load limits and maintenance access.

    Control and Automation

    Cabin or supervised control, automatic operating zones, positioning accuracy, anti-sway, cameras, plant PLC/MES interface and recovery philosophy.

    Power, Destination and Scope

    Voltage, frequency, destination country, governing requirements, delivery term, runway scope, installation, testing, training and required schedule.

    Slab Handling Crane FAQ

    How is slab crane capacity calculated?

    Capacity begins with the maximum slab or slab group and the complete lifting attachment. The contract must state whether rated capacity means net slab payload or gross suspended load. Dynamic and design factors are then applied under the governing engineering basis.

    Which attachment is suitable for hot slabs?

    A temperature-rated mechanical clamp is a common direction where side access and slab geometry permit positive gripping. A magnetic system requires confirmed temperature capability, air-gap conditions and power-loss controls. Final attachment selection follows a documented risk and geometry review.

    Can one clamp handle different slab widths and thicknesses?

    An electrically or hydraulically adjustable clamp can cover an approved operating range. Minimum and maximum dimensions, jaw contact zones, opening clearance, clamping force and locking indication must be defined for every permitted slab family.

    Can a slab handling crane rotate the load?

    Yes. A slewing trolley or rotating lifting beam can change slab orientation. Rotation angle, envelope, inertia, cable routing, stopping accuracy and collision protection are incorporated into the crane and building layout.

    Can the crane operate near 650°C slabs?

    Henan Mine Crane publishes configurations for high-temperature slab exposure up to the stated product limit and documents a 50+50 t case for severe radiant heat. Final approval distinguishes slab surface temperature, ambient air, distance, exposure time and thermal cycling.

    Is an electromagnetic system safe during a power failure?

    Safety depends on the engineered retention and recovery concept. Backup power, monitored holding time, alarms, restricted access and controlled lowering may be required. A generic magnet without a documented power-loss strategy is not an acceptable basis.

    Can the same crane handle billets?

    Possible suitability depends on billet geometry, bundle condition, attachment contact and operating route. A slab clamp is not automatically suitable for billets. The complete billet range and proposed attachment require separate engineering approval.

    What information determines crane duty?

    Load spectrum, moves per hour, travel distance, full-load frequency, operating shifts, annual hours, motion speeds and production consequence determine structural and mechanism duty. Rated tonnage alone is insufficient.

    Can slab warehouses be automated?

    Yes. Automated handling can combine encoders, ranging devices, anti-sway, coordinate storage, slab identification and plant communication. Safe zones, manual recovery, calibration, inventory reconciliation and fault handling form part of the system.

    What should a quotation include?

    A complete quotation identifies capacity basis, attachment, span, lift, duty, speeds, controls, temperature design, safety functions, wheel loads, documentation, testing, delivery boundary, installation responsibility, schedule and exclusions.

    Configure a Slab Handling Crane for the Steel Process

    Submit the slab dimensions and mass range, temperature, attachment preference, handling route, stack plan, throughput, span, lifting height, duty, runway information, power supply, automation scope, destination and delivery boundary. Henan Mine Crane will prepare a project-specific technical configuration and commercial quotation.

    Henan Mine CraneDiscuss your requirements ↗
  • Single Girder Crane

    Single Girder Crane

    Single Girder Crane

    Henan Mine Crane · Engineered Single-Beam Lifting Systems

    Single Girder Crane

    Single-girder overhead, underhung and gantry crane configurations engineered around rated load, span, lifting height, duty, headroom, runway structure and production cycle.

    Henan Mine Crane supplies electric single-girder crane systems for workshops, warehouses, assembly areas, maintenance bays, fabrication plants and material yards. Each proposal defines the bridge, hoist, end carriages, controls, safety functions, runway interface, electrical boundary, delivery documentation and requested site services.

    electric single girder crane operating in an industrial workshop
    A top-running single-girder bridge with an electric hoist provides three-axis load movement across a defined production bay.

    PRIMARY CONFIGURATION

    Top-Running Overhead Crane

    ALTERNATIVE SUPPORT

    Underhung or Gantry

    HOIST OPTIONS

    Wire Rope, Chain & Low Headroom

    CONTROL OPTIONS

    Pendant, Radio, Cabin & PLC

    What Is a Single Girder Crane?

    A single girder crane uses one primary bridge girder to carry the hoisting unit across the working area. In the most common overhead arrangement, an electric wire-rope or chain hoist travels beneath the girder, while powered end carriages move the complete bridge along parallel runway rails. Hoist lifting, cross travel and bridge travel provide vertical, lateral and longitudinal load movement.

    The search term covers more than one support arrangement. A top-running single-girder overhead crane travels on rails installed above runway beams. An underhung single-girder crane travels beneath compatible runway beams. A single-girder gantry crane places the bridge on travelling legs and ground rails. These systems can use similar electric hoists, but their structural interfaces, wheel loads, clearances and site work are different.

    Single-girder construction is commonly selected for general industrial handling where capacity, span, duty and hook-height requirements remain within an efficient electric-hoist design. One girder normally reduces bridge deadweight, wheel reactions, fabrication, freight and erection scope compared with a comparable double-girder bridge. The resulting cost advantage depends on the complete system rather than the girder count alone.

    A single girder is not automatically a light-duty or low-capacity crane. Henan Mine Crane publishes broad product-family ranges, including engineered top-running models extending to high capacities and spans. Practical selection still follows structural calculation, hoist capability, fatigue duty, hook coverage, maintenance access and destination requirements. Where a process trolley, very high duty, greater hook height, walkway access or special attachment cannot be integrated efficiently, a double-girder design may provide the stronger lifecycle solution.

    Components and Operating Principle

    The crane structure, hoist, end carriages, power distribution and controls form one coordinated load-handling system. The main girder transfers the suspended load and bridge self-weight into the end carriages. Wheels transfer vertical and horizontal reactions through the rails into the runway or gantry legs. The selected hoist controls lifting performance and much of the hook approach.

    A purchase specification should identify every interface. Bridge steel and lifting machinery do not automatically include runway beams, rails, support columns, foundations, incoming plant power, installation, test weights or local statutory inspection. Defining these boundaries before quotation prevents equipment-only prices from being compared with complete installed systems.

    detailed components of an electric single girder crane
    Bridge girder, hoist, end carriages, travel drives, electrification and controls operate as one engineered system.

    01 · Main Girder

    A rolled section, composite beam or welded box girder carries the moving hoist and transfers load into the end carriages. Span, capacity, deflection, fatigue and hoist-wheel loading establish the design.

    02 · Electric Hoist

    The lifting unit includes motor, brake, gearbox, drum or load chain, rope or chain guide, hook block and limits. Capacity, lift, reeving, speed and duty must match the handling cycle.

    03 · End Carriages

    Wheel assemblies support the bridge and provide longitudinal travel. Wheel diameter, spacing, rail profile, drives and guide arrangement are coordinated with runway geometry and reactions.

    04 · Electrification

    Conductor bars or festoon systems supply the bridge, while a festoon, cable track or energy chain supplies the moving hoist. Voltage, travel length and environment determine the arrangement.

    05 · Controls and Protection

    Pendant, radio, cabin or PLC controls operate the motions with emergency stop, brakes, upper and lower limits, overload protection and project-specific alarms or interlocks.

    06 · Runway Interface

    Rails, beams, brackets, columns and foundations receive crane forces. New and existing structures require approved wheel loads, side thrust, alignment tolerance and end-stop design.

    Single Girder Crane Configurations

    Top-Running Single-Girder Overhead Crane

    Bridge wheels travel on rails above the runway beams, while the electric hoist normally runs beneath the girder. This is the principal configuration for production workshops, warehouses, fabrication bays and maintenance facilities.

    Underhung Single-Girder Crane

    Bridge end carriages travel on the lower flanges of suspended runway beams. The arrangement can improve floor utilization and end approach, but roof beams, hangers, connections and runway flanges must be verified for crane reactions.

    Low-Headroom Electric-Hoist Crane

    A compact or offset hoist arrangement reduces the vertical distance between runway level and upper hook position. It is developed for low roofs or existing buildings where usable hook height has direct production value.

    Single-Girder Gantry Crane

    Travelling legs support the bridge on ground rails. This configuration serves yards, workshops without elevated runway steel and production zones where building loads should remain independent.

    Intelligent Single-Girder Crane

    Variable-frequency drives, load monitoring, anti-sway, positioning, diagnostic functions and PLC communication can be integrated where motion quality, process repeatability or production data are required.

    Special-Environment Single-Girder Crane

    Explosion-proof, cleanroom, insulated, corrosion-resistant or metallurgical electric-hoist variants require environment-specific equipment, materials, enclosures and protective logic defined by the operating hazard.

    The support arrangement is selected before the final hoist and bridge dimensions are released. Top-running and underhung systems are not interchangeable without structural review. A gantry crane is also a separate project type because leg geometry, ground rails, wind actions, travel lanes and foundations become part of the load path.

    Selection Considerations

    A commercially complete single-girder crane specification begins with the load and operating cycle, then coordinates the lifting mechanism with building geometry and project scope. Capacity alone cannot establish girder size, hoist duty, wheel loads, motor ratings or price.

    01 · Gross Suspended Load

    Include payload, lifting beam, slings, clamps, magnets, grabs and every below-hook component. State maximum, normal and future loads rather than nominal product weight alone.

    02 · Span and Travel Length

    Span is normally the runway rail centreline distance. Runway length determines longitudinal coverage, electrification length and installation quantities.

    03 · Lift and Headroom

    Provide lowest pickup, highest placement, rail elevation, roof clearance, load height and rigging depth. Required hook height must be checked on a dimensioned arrangement.

    04 · Working Duty

    Define lifts per hour, full-load frequency, load spectrum, travel distance, shifts and annual operating hours. These data determine structural and mechanism service requirements.

    05 · Hook Coverage

    End approach, side approach, obstructions and safe operating zones determine whether the hook can reach every required pickup and placement point.

    06 · Building and Runway

    Existing or new runway beams require rail data, support spacing, wheel-load checks, alignment tolerances and an assigned structural approval responsibility.

    07 · Motion Control

    Specify lifting and travel speeds, low-speed range, acceleration, radio or pendant operation, anti-sway, positioning accuracy and any coordinated motion.

    08 · Environment and Compliance

    Temperature, dust, humidity, corrosion, washdown, hazardous-area classification, destination rules and inspection authority influence component and documentation selection.

    Single Girder Crane Compared with Other Configurations

    The most economical structure is the one that meets the complete operating requirement without transferring excessive cost into the runway, building, maintenance plan or production risk. The following comparison separates common arrangements by load path and application.

    Configuration Structural Arrangement Typical Application Commercial Advantage Selection Limit
    Top-running single girder One bridge girder on rails above runway beams; hoist below girder General manufacturing, assembly, warehousing and maintenance Low bridge deadweight, economical structure and broad electric-hoist selection Hook height, duty, span and special accessories must remain practical
    Underhung single girder One bridge girder suspended below compatible runway beams Lighter production bays, extensions and buildings designed for suspended runways Clear floor area and potentially improved end approach Roof reactions, hangers, lower flanges and connections govern feasibility
    Double-girder overhead crane Two bridge girders carrying a hoist trolley or process trolley Higher capacity, longer span, demanding duty and specialized lifting Improved hook height, stiffness, access and process-equipment integration Higher self-weight, wheel loads, fabrication and installation scope
    Single-girder gantry crane One bridge girder supported by travelling legs on ground rails Outdoor yards or facilities without suitable elevated runway support Independent support and optional cantilever coverage Ground rails, foundations, travel lanes, wind and leg clearances are required
    Workstation bridge crane Light enclosed track with floor or ceiling support Ergonomic handling and localized repetitive work Low rolling resistance and precise manual or powered movement Lower capacity and span range; not a substitute for an industrial bridge crane

    A double-girder crane is not automatically superior, and a single-girder crane is not automatically limited to occasional service. The final decision follows calculated bridge behavior, selected hoist duty, usable hook envelope, required access and total installed cost.

    Technical Specification Framework

    Henan Mine Crane maintains several single-girder product families. Published ranges describe available engineering platforms rather than guaranteed combinations. Final capacity, span, lifting height, speeds, working class and wheel loads are confirmed on the approved general arrangement and technical schedule.

    Product Family Capacity Position Span Position Lifting Height Working Class / Control Electrical Position
    Top-running single-girder bridge family Published table: 3.2–80 t 4–31.5 m Lifting height configured for the site A5 published base; project duty confirmed 220–690 V, 3-phase, 50–60 Hz
    Intelligent electric-hoist overhead family 1–32 t 7.5–31.5 m 6–30 m A5–A6 Configured for destination grid
    Underhung single-girder family 0.5–20 t 3–16 m 6 m, 9 m, 30 m or customized A3–A5 Configured for destination grid
    European single-girder gantry family 1–32 t or customized 6–35 m 4–20 m A3–A5 220–660 V, 50–60 Hz available
    Control and protection options Matched to rated load Matched to bridge geometry Upper and lower limits coordinated with lift Pendant, radio, cabin or PLC IP54/IP55 options within published overhead family

    A capacity shown within a family range does not confirm suitability at every span or duty. Long spans, high capacities, severe load spectra and demanding hook-height requirements require a project-specific bridge and hoist check. The single-girder bridge crane product data supports preliminary selection; the contract specification and approved drawings control the delivered equipment.

    Hoist Selection, Headroom and Hook Coverage

    The hoist is the principal operating mechanism on a single-girder crane. Its body position, trolley wheelbase, drum or chain arrangement, hook block and reeving determine lifting speed, upper hook position, side approach and maintenance envelope. A low acquisition price has limited value when the hook cannot reach the required machine, rack or assembly position.

    Electric Wire-Rope Hoist

    Common industrial selection for broader capacities, lifting heights and speed options. Drum capacity, rope reeving, fleet angle, brake, gearbox and trolley duty are matched to the operating cycle.

    Electric Chain Hoist

    Compact solution for lighter loads and localized handling. Chain container, reeving, duty, lifting speed and upper-limit arrangement must fit the available vertical envelope.

    Low-Headroom Hoist

    Offset geometry positions the hoist body around the girder to improve the highest hook elevation. The complete dimensional drawing must also preserve inspection and removal access.

    Variable-Frequency Motion

    VFD control supports smooth acceleration, controlled low speed and reduced load swing. Required minimum speed and positioning performance should be stated numerically.

    Two-Hoist Handling

    Two lifting units can support long loads where permitted by the bridge design. Individual capacities, combined loading, hook spacing and allowed control modes must be defined.

    Below-Hook Attachment

    Lifting beams, C-hooks, clamps, magnets and grabs add suspended weight and change load geometry. Attachment mass is included in crane capacity and headroom calculations.

    Approval drawings should state span, rail elevation, crane top clearance, highest and lowest hook positions, left and right hook approaches, end approaches, bridge depth and maintenance clearances. These dimensions establish usable coverage more accurately than capacity and lifting height alone.

    Runway, Building and Electrical Interface

    A bridge crane and its runway form one structural system. The crane supplier provides crane weight, maximum wheel loads, wheel spacing, horizontal forces and relevant operating data. The responsible structural party verifies runway beams, brackets, columns, connections, foundations and building stability. Existing runway reuse requires condition, geometry and capacity checks before manufacturing dimensions are frozen.

    Rail and Alignment

    Rail section, gauge, straightness, elevation, joint condition and end stops influence wheel contact, skewing and travel quality. Crane runway tolerances are normally tighter than general building-steel tolerances.

    Wheel Loads and Reactions

    Maximum and minimum wheel loads, impact, side thrust and braking forces are assessed with the crane in governing hook positions. A replacement crane can impose different reactions at the same rated capacity.

    Clearance and Access

    Roof bracing, ducts, lights, sprinklers, cable trays and adjacent equipment require clearance throughout bridge travel. Safe access is required for hoist, drives, panels and wearing parts.

    Incoming Power

    Voltage, frequency, phase, isolation point, grounding and available fault level are confirmed before electrical design. Runway conductor scope and the interface to plant power are assigned in the offer.

    Freestanding Runway

    Independent columns can avoid loading an existing building. Column spacing, floor use, foundations, aisle traffic and future expansion become project design inputs.

    Underhung Support

    Suspended systems require beam-flange, hanger, connection and roof-reaction checks. The ability to hang a static load from a roof does not by itself establish crane runway suitability.

    Industrial Applications

    Machining and Fabrication

    Moves plate, profiles, fixtures, machine parts and welded assemblies between cutting, machining, welding, inspection and dispatch stations.

    Assembly and Production

    Supports component positioning, subassembly transfer and line-side material supply where smooth low speed and accurate hook approach improve process control.

    Warehouse and Logistics

    Handles machinery, tools, dies, steel products and unit loads across storage bays without consuming the permanent floor lanes required by mobile lifting equipment.

    Maintenance Facilities

    Provides coverage for motors, pumps, gearboxes, vehicle components and production machinery during removal, inspection and reinstallation.

    Precast and Building Materials

    Transfers molds, reinforcement assemblies and finished components when load weight, lifting points, span and operating environment suit an electric-hoist bridge or gantry system.

    Controlled or Hazardous Areas

    Cleanroom, explosion-proof, corrosion-resistant or insulated variants are configured only after the required cleanliness, zone, gas or dust group, temperature class and material restrictions are declared.

    Standard single-girder cranes are intended for defined general-service conditions. Molten metal, suspended permanent magnets, high-temperature loads, explosive atmospheres, corrosive exposure and unattended automation require dedicated product selection and risk controls rather than additions to a conventional specification.

    Project Experience: 300+ Intelligent Cranes for XCMG Manufacturing

    single girder crane installed for intelligent industrial manufacturing
    Single-girder bridge systems can be integrated with controlled motion and production-line requirements for industrial manufacturing.

    Henan Mine Crane reports the successive supply of more than 300 intelligent cranes of various types for XCMG manufacturing operations. The equipment supports assembly and structural-component movement across engineering-machinery production processes, with project configurations covering bridge, gantry and specialized crane forms.

    The program emphasizes high-precision positioning, digital controls, remote monitoring, fault warning and production-system integration. Reported project capacities extend from 5 t to 1,000 t across the complete mixed fleet. This range confirms that one factory program can require several crane architectures rather than one repeated model.

    For a single-girder package within a comparable manufacturing environment, the transferable engineering priorities are load-path definition, repeatable low-speed motion, verified hook coverage, appropriate working duty, maintainable electrification and consistent control logic. The final design remains specific to each bay, capacity and production task.

    View Project Experience →

    Engineering, Manufacturing, Delivery and Acceptance

    automated crane girder welding workstation at Henan Mine Crane
    Controlled welding, dimensional inspection and documented testing support bridge geometry and configuration integrity.

    A reliable single-girder crane project connects approved operating data to structural design, mechanism selection, fabrication, inspection, packing, erection and handover. General arrangement drawings and interface loads are approved before bridge dimensions or runway connections are released.

    Manufacturing control can include material identification, welding procedures, dimensional inspection, mechanism records, electrical diagrams, coating checks and factory functional tests. Site control can include rail survey, bridge assembly, electrical verification, protective-device settings, no-load checks, rated-load testing and commissioning records.

    Supply Package Typical Content Technical Control Commercial Boundary
    Crane bridge package Main girder, end carriages, wheels, drives, buffers, connections and specified access items Capacity, span, duty, deflection basis and wheel reactions approved Assembly hardware and shipping splits listed
    Hoist and lifting equipment Hoist, trolley, rope or chain, hook block, brakes, limits and overload protection Lift, headroom, speeds, reeving and service duty confirmed Below-hook attachment and rigging boundary stated
    Electrical and controls Panels, pendant or radio, VFDs, crane wiring, alarms and moving electrification Voltage, frequency, control philosophy and enclosure rating confirmed Incoming supply and runway feed responsibility assigned
    Runway and supports Rails, clips, beams, brackets, columns, stops and foundations where contracted Travel length, rail section, support spacing and structural reactions approved Building and civil work explicitly included or excluded
    Documents and inspection Drawings, manuals, certificates, electrical diagrams, inspection records and packing documents Language, approval stages and witness points agreed Factory and site acceptance criteria identified
    Logistics and site services Export packing, freight, unloading, erection, alignment, wiring, testing and training as contracted Incoterm, access, lifting equipment, labor and test weights assigned Taxes, permits and local inspection responsibility stated

    Single Girder Crane Price and Total Project Cost

    Public international pricing shows why a single figure cannot represent every single-girder crane. A component kit, complete bridge package and installed system contain different scope. Capacity, span, lift, duty, hoist, controls, runway, freight and site access materially change the project value.

    Budget Position Indicative Public Market Position Typical Included Basis Common Exclusions or Variables
    5 ton underhung crane kit with hoist Approximately US$25,000 Commercial component-kit position with hoist Bridge beam, runway, support structure, freight, installation and testing require confirmation
    5 ton top-running crane kit with hoist Approximately US$27,700 Commercial top-running component-kit position Girder steel, runway, electrification, freight, erection and local electrical work may be separate
    5 ton base single-girder bridge crane Approximately US$40,000 Published North American benchmark for a base bridge, trolley or hoist package at 40 ft span or less Installation is excluded in the stated benchmark; runway and building work depend on site
    5 ton packaged single-girder crane with hoist Approximately US$47,600–52,300 Current public retail positions for specified packaged bridge-crane configurations Span, runway, support steel, shipping, installation, electrical feed and acceptance vary
    10 ton installed single-girder bridge crane Approximately US$65,000 Representative North American installed position Actual span, runway condition, access, permits, local labor and load test affect final cost
    Custom high-duty or special-environment crane Project quotation Engineered bridge, hoist, controls and protection for the declared process Runway, automation, certification, freight, site work and local inspection must be defined

    Commercial comparison: capacity, span, lifting height, working class, speeds, hoist model, controls, bridge steel, runway scope, electrification, documentation, freight, installation and testing should be normalized before quotations are compared. A low kit price is not equivalent to a commissioned crane system.

    Indicative positions were checked against public market information in September 2026 and are intended for preliminary capital planning. They are not fixed Henan Mine Crane quotations. Currency, destination, steel cost, specification and site conditions can change contract value.

    Quote Information and Frequently Asked Questions

    A complete request for quotation should provide maximum gross suspended load, normal load spectrum, load dimensions, lifting attachment, span, runway length, lifting height, rail elevation, headroom, operating cycle, required speeds, control method, environment, power supply, building or runway information, destination, delivery term and required installation boundary.

    Load and Process Data

    Maximum and routine loads, attachment mass, dimensions, center of gravity, lifting points, cycles per hour, travel route and production consequence.

    Building and Coverage Data

    Span, runway length, rail elevation, highest hook position, roof obstacles, column spacing, hook approaches and existing runway details.

    Operating and Control Data

    Working shifts, load spectrum, lifting and travel speeds, low-speed positioning, pendant, radio, cabin, PLC and anti-sway requirements.

    Commercial and Site Data

    Destination, voltage, Incoterm, governing requirements, inspection authority, installation resources, test weights and commissioning scope.

    What is the difference between a single girder crane and a single girder overhead crane?

    Single girder crane is the broader term. A single-girder overhead crane travels on elevated runway beams, while a single-girder gantry crane is supported by legs travelling on ground rails.

    How much does a single girder crane cost?

    Current public positions range from approximately US$25,000–27,700 for selected 5 t component kits with hoists to approximately US$40,000 for a base 5 t bridge crane and US$47,600–52,300 for listed packaged configurations. Installed and engineered project values depend on scope.

    When should a double-girder crane be selected?

    Double girders are considered when capacity, span, duty, hook height, stiffness, trolley arrangement, service access or process equipment cannot be integrated efficiently into a single-girder system.

    Can a single-girder crane use an existing runway?

    Reuse is possible after structural capacity, rail section, gauge, alignment, end stops, clearances and proposed wheel loads are verified. Matching rated capacity alone does not confirm compatibility.

    Which hoist is suitable for a single-girder crane?

    Wire-rope hoists cover a broad range of industrial capacities, lifts and speeds. Chain hoists serve lighter compact handling. Low-headroom hoists improve upper hook elevation where building height is restricted.

    Can a single-girder crane be supplied with radio remote control?

    Pendant and radio control are common options. Cabin, PLC, variable-frequency motion, anti-sway, load monitoring and positioning functions are configured when justified by the process.

    Does the crane quotation include runway and installation?

    Runway steel, rails, columns, foundations, freight, erection, electrical feed, test weights and local inspection are included only when expressly listed. Every offer should contain a scope and exclusion schedule.

    What documents support acceptance?

    The handover package can include approved drawings, wheel-load data, electrical diagrams, manuals, component records, inspection results, factory test documents, commissioning settings and site load-test records.

    Request a Single Girder Crane Quote

    Submit the maximum gross load, span, lifting height, runway length, duty cycle, hook coverage, building information, power supply, control requirements, operating environment, destination and required supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.

    Henan Mine CraneDiscuss your requirements ↗
  • Shipyard Gantry Cranes

    Shipyard Gantry Cranes

    Shipyard Gantry Cranes

    Henan Mine Crane · Engineered Shipbuilding Lifting Systems

    Shipyard Gantry Cranes

    Henan Mine Crane engineers rail-mounted shipyard gantry cranes for hull-block assembly, section turning, dock erection, marine equipment installation, ship repair and offshore module handling. Each crane is configured around the heaviest lifting case, block geometry, required turning sequence, dock span, runway loads, coastal environment and project acceptance requirements.

    The current product family includes 100 t, 200 t, 250 t and 450 t configurations, with larger combined-lifting arrangements available for major shipbuilding programs. Dual-trolley, upper-and-lower-trolley and multi-hook systems can be developed for controlled section lifting and turning.

    Henan Mine Crane shipyard gantry crane for hull block assembly
    Rail-mounted shipbuilding gantry crane configured for large hull-section lifting and assembly. Final capacity, span, lifting height and trolley arrangement are established by the approved project design.

    LISTED CAPACITY FAMILY

    100–450 t or Custom

    TYPICAL SPAN FAMILY

    40–97 m or Custom

    TYPICAL LIFTING HEIGHT

    35–70 m or Custom

    LISTED DUTY DATA

    Project-Specific A5 or A7–A8

    What Is a Shipyard Gantry Crane?

    A shipyard gantry crane, also called a shipbuilding gantry crane or shipyard Goliath crane, is a large rail-mounted crane that spans a fabrication area, slipway or dry dock. Unlike a general yard crane, it is engineered to lift long and flexible hull blocks, coordinate several lifting points, turn sections in the air when required, and place modules at controlled assembly positions.

    The crane structure commonly combines a double-girder bridge with one rigid leg and one flexible leg. This arrangement accommodates large spans while controlling structural restraint. The lifting system may use upper and lower trolleys, two coordinated trolleys or several hooks, depending on the block-turning method and required lifting capacity.

    Hull Block Assembly

    Lift decks, bulkheads, side shells and preassembled hull sections between fabrication, alignment and welding positions.

    Dry Dock Erection

    Position bow, stern, engine-room and superstructure modules during final hull erection and pre-launch construction.

    Ship Repair and Conversion

    Remove or install propulsion equipment, rudders, propellers, deck machinery and conversion modules during major dock work.

    Offshore Module Handling

    Handle selected vessel, platform, FPSO and offshore wind modules within a defined fabrication and assembly corridor.

    Selection Considerations

    01 / LOAD CASE

    Block Mass and Load Distribution

    Define maximum and typical block mass, dimensions, centre of gravity, lifting lugs, rigging mass and allowable local loads. Individual hook, trolley, combined and turning capacities must remain distinct.

    02 / TURNING PLAN

    Section Rotation Method

    Establish pickup points, hook spacing, required rotation angle, load transfer between hooks, control sequence and permitted forces at every stage of the turn.

    03 / GEOMETRY

    Span, Lift and Hook Coverage

    Map rail centres, dry-dock width, highest module, lowest hook position, side approaches, cantilever needs and all interference zones.

    04 / DUTY

    Operating Cycle and Design Life

    State lifts and turns per shift, load spectrum, travel distances, operating hours, planned vessel program and future block-size changes.

    05 / CIVIL WORK

    Runways and Foundations

    Coordinate wheel loads, wheel spacing, horizontal forces, storm anchoring, rail tolerances, drainage and geotechnical information with the civil design.

    06 / COASTAL SITE

    Wind and Corrosion Basis

    Provide site wind data, storm procedures, temperature, salt exposure, humidity, rainfall and coating-life requirements.

    07 / CONTROL

    Power and Operating Philosophy

    Define site supply, cable route, control stations, variable-speed motions, synchronized lifting, communications and data interfaces.

    08 / DELIVERY

    Transport and Erection Strategy

    Confirm shipment segmentation, route limits, unloading method, erection cranes, temporary works, assembly space and site test responsibilities.

    The lifting-capacity schedule must identify the permissible load for every operating case. The arithmetic sum of several hook or trolley ratings does not automatically establish the crane’s combined lifting or section-turning capacity.

    Shipyard Gantry Cranes Compared with Other Gantry and Port Cranes

    Crane type should follow the handled object and operating process. A shipyard Goliath crane is selected for large hull blocks and dock assembly; container and harbor cranes use different handling systems, motion requirements and acceptance criteria.

    Crane Configuration Primary Load Operating Area Principal Selection Difference
    Shipyard Gantry Crane Hull blocks, superstructures and large marine modules Shipyard fabrication area, slipway or dry dock Very large span, coordinated hooks and engineered section-turning cases
    Double-Girder Gantry Crane Machinery, steel structures and general heavy cargo Industrial yard or assembly bay General hook handling without the complete ship-block turning system
    Rail-Mounted Container Gantry Crane ISO containers under a dedicated spreader Container terminal or intermodal yard Container stacking geometry, anti-sway and terminal operating cycle
    Rubber-Tyred Gantry Crane Containers or defined industrial loads Paved yard with block-to-block mobility Tyre travel and steering replace fixed shipyard rails
    Container Straddle Carrier Individual containers or compatible unit loads Terminal transfer route Mobile pickup and transport rather than full dock-span coverage
    Portal Harbor Crane Ship cargo, grabs, hooks or project cargo Quay or terminal apron Slewing and luffing cargo transfer instead of hull-block assembly

    Hull Block Lifting, Turning and Positioning

    Shipyard Goliath crane with coordinated trolley arrangement for hull section handling
    Coordinated trolley and hook arrangements can support hull-section lifting, load transfer and controlled turning when each operating stage is included in the approved lift plan.

    1. Establish Every Load Case

    Engineering starts with the block in its fabrication position and follows it through pickup, initial suspension, rotation, load transfer, final orientation and landing. Hook forces can change substantially as the centre of gravity moves relative to the lifting points.

    2. Select the Trolley and Hook Arrangement

    Upper-and-lower trolleys can pass or work at different elevations. Two trolleys can distribute a long block across separated lifting points. Multi-hook systems require defined individual capacities, combined capacity, hook spacing and permitted simultaneous movements.

    3. Control Motion and Synchronization

    PLC supervision and variable-frequency drives can coordinate selected motions, limit speed during critical stages and monitor deviations. The allowable synchronization tolerance and response to a sensor, drive or communication fault must be stated in the technical agreement.

    4. Verify the Lifting Attachment

    Spreader beams, equalizing devices, slings, shackles and block lifting lugs form part of the load path. Their masses reduce available payload, and their geometry affects headroom, hook approach and section stability.

    Shipyard Gantry Crane Specifications

    The current Henan Mine Crane product data identifies the following available ranges. These values describe configurable equipment, not one automatic model combination. Final dimensions, speeds, duty, wind criteria, power supply, wheel loads and acceptance tolerances are established in the approved project documents.

    Parameter Available Product Data Project Definition
    Lifting capacity 100 t, 200 t, 250 t, 450 t or custom Individual hook, trolley, combined-lifting and turning ratings
    Span 40–97 m in the principal family; separate listed configurations extend to 185 m Rail centre distance, leg clearances, cantilevers and structural restraint
    Lifting height 35–70 m in the principal family; larger listed configurations use project-specific upper and lower hook travel Highest and lowest hook positions including rigging and load depth
    Working class A7–A8 in the principal family; separate listed large configurations identify A5 Selected from load spectrum, cycles, travel and required design basis
    Hoisting speed Main hoist 0.5–10 m/min; auxiliary hoist 1–20 m/min in the principal data Full-load, no-load, positioning and turning-stage speeds
    Travel speed Trolley 5–30 m/min; crane long travel 10–40 m/min in the principal data Loaded and unloaded speeds, acceleration, skew control and stopping distance
    Operating temperature −20°C to +40°C in the principal product data Site minimum, maximum, humidity, salt exposure and solar heating
    Power supply 3-phase 380 V, 50 Hz; 400 V or 415 V available; listed very large configurations use 10 kV, 50 Hz Site voltage, fault level, feeder, cable reel or conductor interface
    Control modes Cab, remote console and wireless remote operation Permitted operating stations, authority transfer, emergency control and communications

    Separate listed configurations include two-trolley combined lifting capacities from 150 t to 1,000 t and section-turning capacities from 100 t to 800 t. These are independent engineered configurations and must not be treated as additions to the principal 100–450 t family.

    Representative Shipyard and Shipbuilding Crane Projects

    Shipbuilding lifting projects range from one very large dock-spanning Goliath crane to coordinated crane packages serving fabrication and final-assembly workstations. The following project cases demonstrate both requirements. Client identities remain confidential where project disclosure is restricted.

    450 ton large-span shipbuilding gantry crane project by Henan Mine Crane
    Large-span shipbuilding gantry crane engineered for heavy hull-section handling across a dedicated shipyard assembly area.

    PROJECT CASE 01 · HEAVY HULL-BLOCK HANDLING

    450 t Large-Span Shipbuilding Gantry Crane

    CAPACITY

    450 t

    SPAN

    97 m

    LIFTING HEIGHT

    70 m

    Henan Mine Crane developed this configuration for a large shipbuilding application requiring heavy hull sections to be lifted and positioned across a wide assembly footprint. The 97 m span and 70 m lifting height place structural stiffness, wheel-load distribution, skew control, wind restraint and erection planning at the centre of the design process.

    The completed configuration demonstrates why rated capacity cannot be evaluated independently. Hook arrangement, combined lifting cases, block geometry, runway tolerances, coastal protection, maintenance access and storm parking provisions must be developed as one operating system.

    custom crane package for large cruise ship final assembly
    Multi-crane lifting package supporting component movement and controlled assembly across large cruise ship production workstations.

    PROJECT CASE 02 · SHIPBUILDING PRODUCTION PACKAGE

    12-Crane Package for Large Cruise Ship Final Assembly

    PACKAGE

    12 Cranes

    LISTED CAPACITIES

    5 t and 10 t

    APPLICATION

    Final Assembly

    The equipment package supports staged handling of steel structures, subassemblies, machinery and outfitting materials within a large cruise ship final-assembly operation. Multiple crane specifications were assigned to separate production zones so that load capacity, hook approach, positioning speed and workstation layout could match each task.

    This case concerns a coordinated shipbuilding crane package rather than one 450 t Goliath crane. It demonstrates the wider plant-planning requirement: heavy dock assembly and lighter component workstations often require different crane types under one material-flow strategy.

    Review the Cruise Ship Assembly Project

    Comparable Project Scope for RFQ Review

    A technically comparable project case should identify the handled load, individual and combined capacities, span, lifting height, trolley and hook arrangement, working class, wind basis, control philosophy, runway interface and delivery scope. A similar capacity alone does not establish comparable engineering complexity.

    Structure, Runways and Coastal-Site Design

    Rigid and Flexible Leg Arrangement

    A rigid leg transmits longitudinal and transverse forces while the flexible leg accommodates the deformation behavior of a very wide bridge. Girder geometry, leg stiffness, wheel groups and connections are evaluated as one structural system.

    Runway and Foundation Interface

    The crane proposal must provide wheel loads, wheel spacing, longitudinal and transverse actions, rail requirements and anchoring loads. Civil design must address soil conditions, differential settlement, rail alignment, drainage and access for inspection.

    Wind Protection and Storm Parking

    Anemometers, alarms, service brakes, rail clamps, storm anchors and tie-down provisions are selected around the governing wind basis. Current product data identifies 20 m/s operating and 55 m/s non-operating values for a specified configuration; contractual thresholds require confirmation against site wind data and the applicable design standard.

    Marine Corrosion Protection

    Surface preparation, coating system, dry-film thickness, edge treatment, enclosed-space protection, fastener materials and electrical enclosures must match the coastal exposure category and required coating life. Inspection access and touch-up procedures form part of lifecycle planning.

    Henan Mine Crane rail-mounted shipbuilding gantry crane at a coastal facility
    Large-span shipyard crane structure operating on dedicated ground-level rails. Wind, corrosion, drainage, rail geometry and storm anchoring are project-level design inputs.

    Control, Monitoring and Safety Functions

    Coordinated Motion Control

    PLC and variable-frequency control can coordinate selected hooks, trolleys and long-travel drives. The control narrative should define permissible simultaneous motions, speed limits and recovery from a failed device.

    Load and Position Monitoring

    Load values, hook positions, trolley positions, crane travel, wind speed and selected drive conditions can be displayed and recorded. Alarm and shutdown limits require defined acceptance tests.

    Hoisting and Travel Protection

    Overload protection, hoisting limits, travel limits, brakes, buffers, emergency stops, anti-collision and overspeed protection are specified for the selected mechanisms and applicable requirements.

    Skew Control and Rail Protection

    Long-span crane travel requires coordinated drives, rail-position monitoring where specified, wheel-flange protection and clear maintenance criteria for alignment and skew trends.

    Current product data lists synchronization accuracy up to ≤3 mm for a specified coordinated-lifting configuration. The final tolerance, measuring method, load condition, permitted duration and response to deviation must be defined contractually before this value becomes an acceptance requirement.

    Engineering, Manufacturing and Documentation

    A shipbuilding crane purchase requires an agreed design basis and inspection plan before fabrication. Henan Mine Crane can establish the equipment scope around the shipyard layout, lift cases, local regulations and required project documents.

    Design Deliverables

    • Design criteria and load-case schedule
    • General arrangement and hook-coverage drawings
    • Wheel loads and civil-interface data
    • Electrical architecture and control narrative

    Manufacturing Controls

    • Material identification and traceability scope
    • Approved welding and inspection plan
    • Dimensional control and trial-assembly checks
    • Surface preparation and coating inspection

    Testing and Handover

    • Factory functional and control tests
    • Site commissioning and applicable load tests
    • Operating and maintenance manuals
    • Inspection records and spare-parts schedule

    Manufacturing capability and production facilities are presented in the Henan Mine Crane Factory Scene Display. The contract should identify which inspections are witnessed, which records are supplied and which criteria govern acceptance.

    Delivery, Installation and Commissioning

    Segmented Delivery Planning

    Girder and leg segmentation must match road, port, vessel and site lifting limits. Packing, lifting points, temporary supports and storage conditions are agreed before dispatch.

    Erection and Rail Verification

    Site work includes rail survey, temporary stability, structural assembly, drive alignment, electrical installation and storm-restraint commissioning under the approved erection method.

    Functional and Load Testing

    Commissioning verifies individual mechanisms, coordinated movements, limits, brakes, alarms, emergency functions and applicable load cases. A section-turning demonstration requires an agreed test method.

    Lifecycle Access and Spares

    Platforms, access routes, isolation points and component-removal paths should be reviewed during design. Initial spares and long-term critical spares follow the operating and maintenance strategy.

    Shipyard Gantry Crane Price and Project Cost

    An early equipment budget of approximately US$200,000–US$1,000,000+ may be used for initial screening of new heavy shipbuilding gantry cranes. This range is not a fixed Henan Mine Crane selling price and does not represent an installed 450–1,000 t long-span Goliath system.

    Large shipyard cranes are individually engineered. Very high capacity, dual-trolley lifting, section-turning systems, long spans, high lifting heights, high-voltage power and extensive coastal protection can move the project into a multi-million-dollar budget before foundations, rails, international transport, erection and commissioning are complete.

    Cost Package Typical Inclusions Principal Cost Drivers
    Crane Equipment Bridge, legs, wheel groups, trolleys, hoists, controls and specified safety functions Capacity, span, height, duty, trolley layout, wind and corrosion requirements
    Lifting and Turning System Multiple hooks, spreader beams, equalizing equipment, sensors and coordinated controls Block geometry, hook spacing, turning load cases and acceptance tolerance
    Civil and Electrical Interfaces Foundations, rails, storm anchors, drainage, substation, feeder and power distribution Soil, wheel loads, runway length, voltage and site construction conditions
    Delivery and Site Work Packing, inland transport, ocean freight, unloading, erection, tests, training and handover Shipment size, route, installation cranes, labor, schedule and test scope

    A valid quotation comparison uses the same capacity definitions, lift cases, span, height, working class, wind basis, coating system, control scope, power interface, documentation, delivery term and site-service boundary. Equipment-only pricing is not directly comparable with a complete installed-system proposal.

    Shipyard Gantry Crane FAQ

    What is the difference between a shipyard gantry crane and a general gantry crane?

    A shipyard crane is designed around hull blocks, very large spans, coordinated lifting points and possible section turning. A general gantry crane normally performs single-hook or main-and-auxiliary-hook handling without the complete shipbuilding process package.

    How much does a shipyard gantry crane cost?

    An initial new-equipment screening range is approximately US$200,000–US$1,000,000+. Large 450–1,000 t long-span cranes with coordinated lifting and complete site works require individual engineering and can become multi-million-dollar projects.

    Can one crane lift and turn a complete hull block?

    Yes, where the crane, trolley arrangement, hooks, lifting attachments and control system are engineered for every stage of the turning operation. The turning capacity can be lower than the combined straight-lifting capacity.

    Why are rigid and flexible legs used?

    The rigid leg provides lateral restraint, while the flexible leg accommodates the deformation behavior of a very long bridge and reduces unwanted restraint. Final geometry follows the structural analysis and site layout.

    What information is required for hull-block turning design?

    Required data includes block mass, dimensions, centre of gravity, lifting-lug positions, allowable forces, rigging arrangement, initial and final orientations, turning sequence, landing supports and environmental limits.

    Can the crane operate in coastal wind and salt spray?

    It can be configured for the specified coastal environment. The design must state operating and storm wind criteria, parking procedure, clamps and anchors, coating system, enclosure ratings, materials and inspection intervals.

    Are rails and foundations included in the crane price?

    Only when expressly stated. The commercial schedule should separate crane equipment, rails, civil works, storm anchors, electrical infrastructure, transport, erection, commissioning and tests.

    What power supply is required?

    Power depends on crane size and site infrastructure. Current product data includes low-voltage three-phase supplies for selected models and 10 kV, 50 Hz for very large listed configurations. The final electrical design must match the destination grid and operating demand.

    How is synchronized lifting accepted?

    The technical agreement should state the measured variable, tolerance, load condition, travel distance, sampling method, alarm threshold and shutdown response. Factory and site tests then verify the agreed control performance.

    What information is required for a formal quotation?

    Provide maximum and typical loads, turning cases, block drawings, span, lifting height, runway length, dock cross-section, duty, wind and corrosion data, power supply, project location, required standards, inspection plan and delivery and installation scope.

    Request A Shipyard Gantry Crane Quote

    A project-specific proposal is prepared from the ship block data, dock layout, operating cases and required commercial boundary. The RFQ should include:

    • Maximum and typical block loads, dimensions, centres of gravity and lifting points.
    • Straight-lifting, combined-lifting and section-turning cases.
    • Span, lifting height, runway length, dock cross-section and required hook coverage.
    • Operating cycle, wind data, coastal exposure and site power supply.
    • Project location, governing standards, inspections, delivery terms and installation scope.
    Henan Mine CraneDiscuss your requirements ↗