分类: Selection Guides

Equipment selection by lifting capacity, technology and working environment.

  • Forging Crane Systems

    Forging Crane Systems

    Forging Crane Systems

    Henan Mine Crane · Engineered Forge-Shop Lifting Systems

    Forging Crane Systems

    Heavy-duty overhead cranes engineered to lift, transfer, turn and position hot ingots, billets, dies and forged components in open-die forging, press, hammer and heat-treatment facilities.

    Henan Mine Crane configures each forging crane from the maximum gross suspended load, workpiece temperature, press or hammer sequence, turning method, impact and load spectrum, cycle frequency, workshop geometry, required positioning performance and local compliance route. Systems can combine main and auxiliary hoists, powered turning devices, tongs or clamps, heat shielding, variable-frequency drives, cameras and production-line coordination.

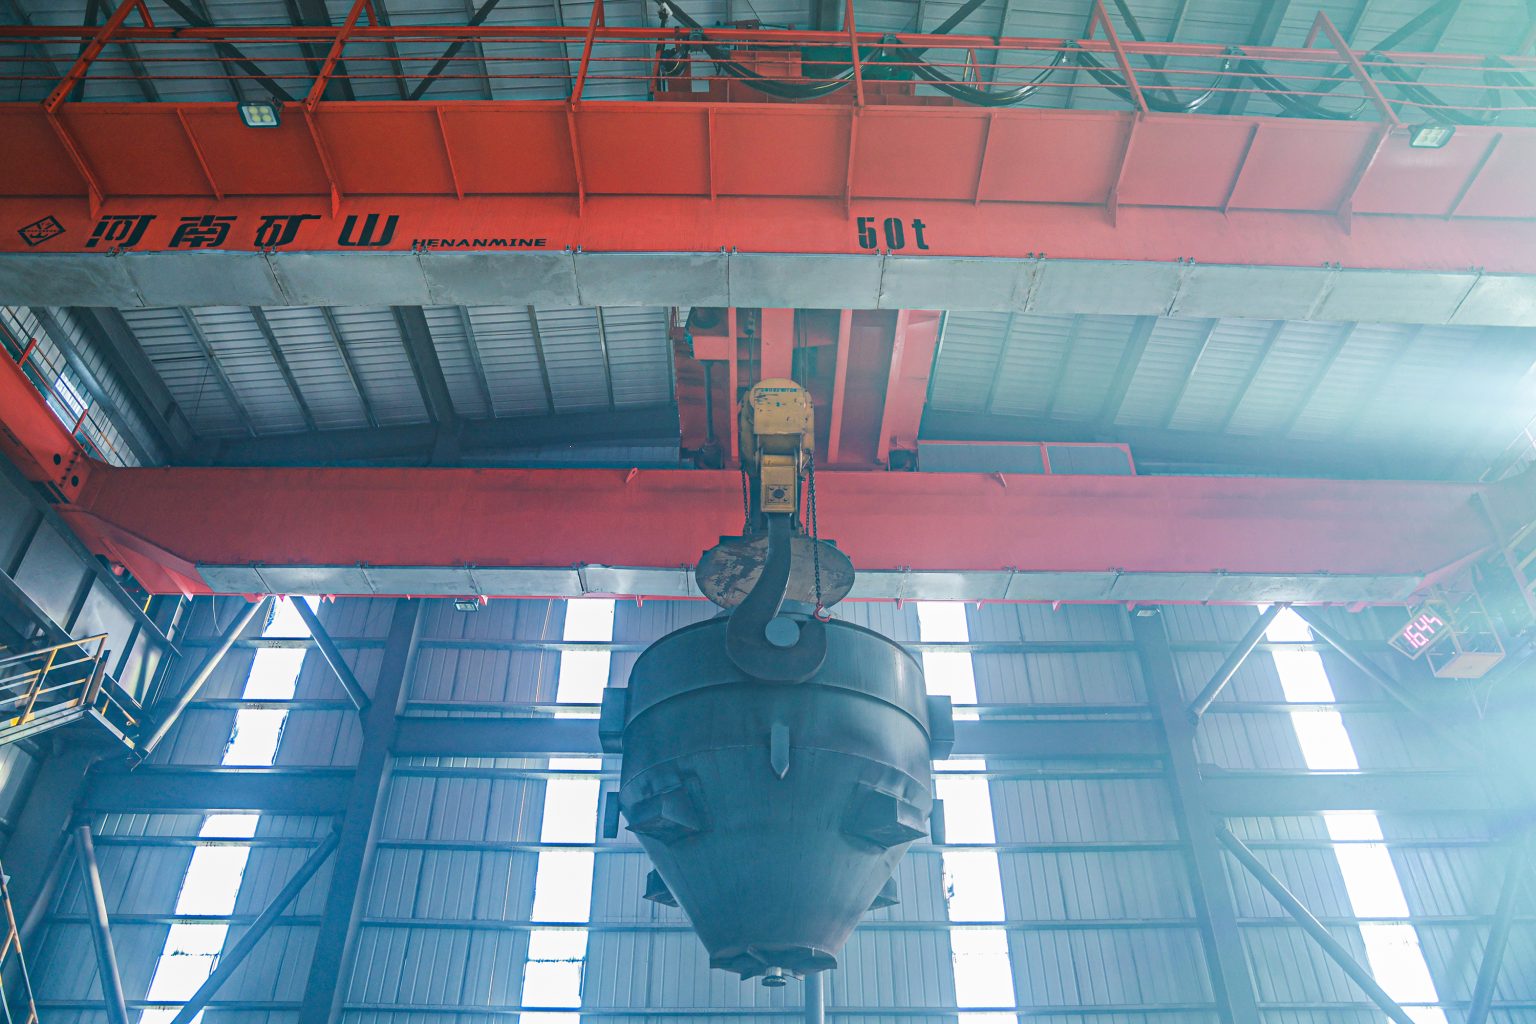
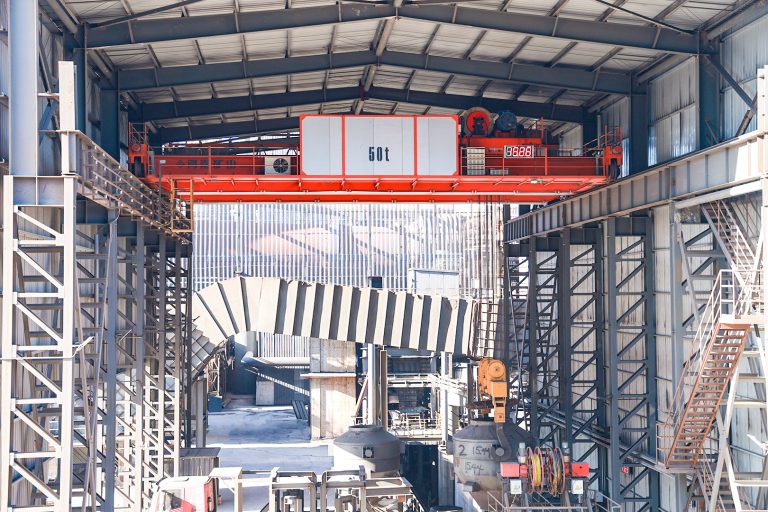
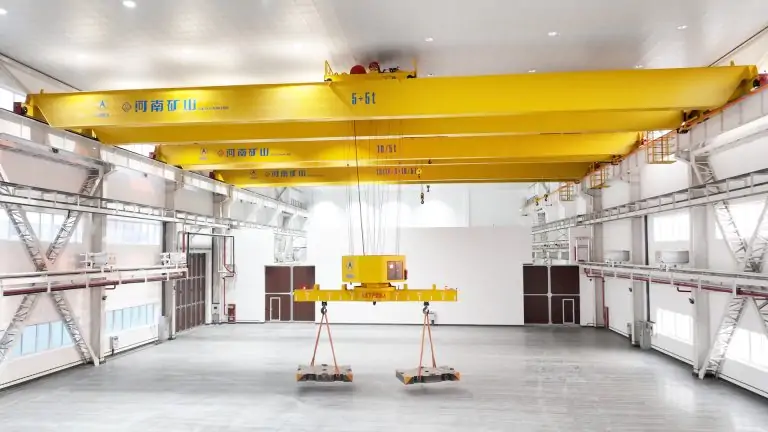
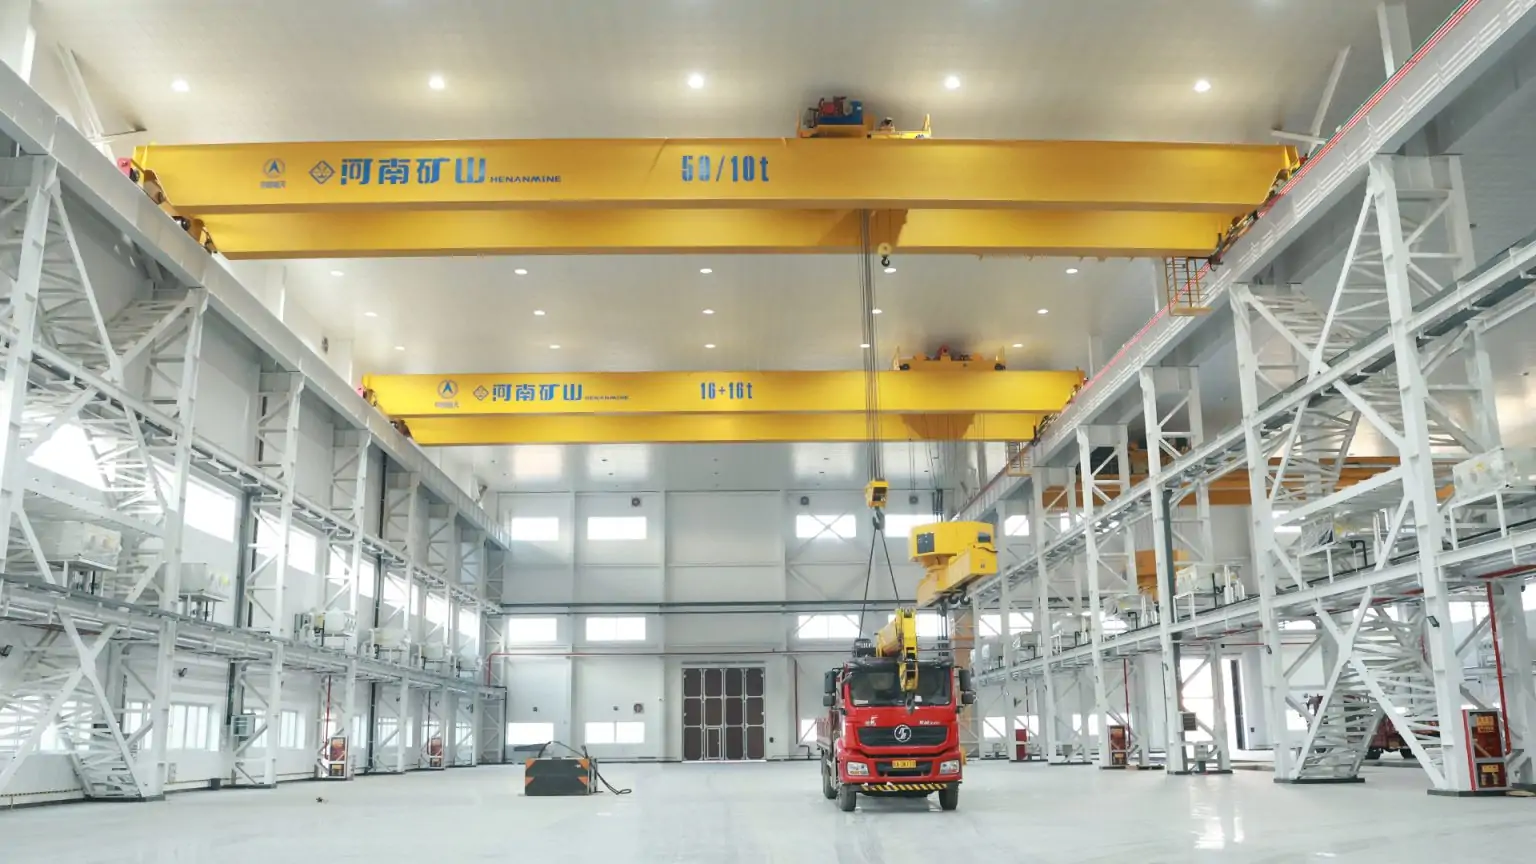
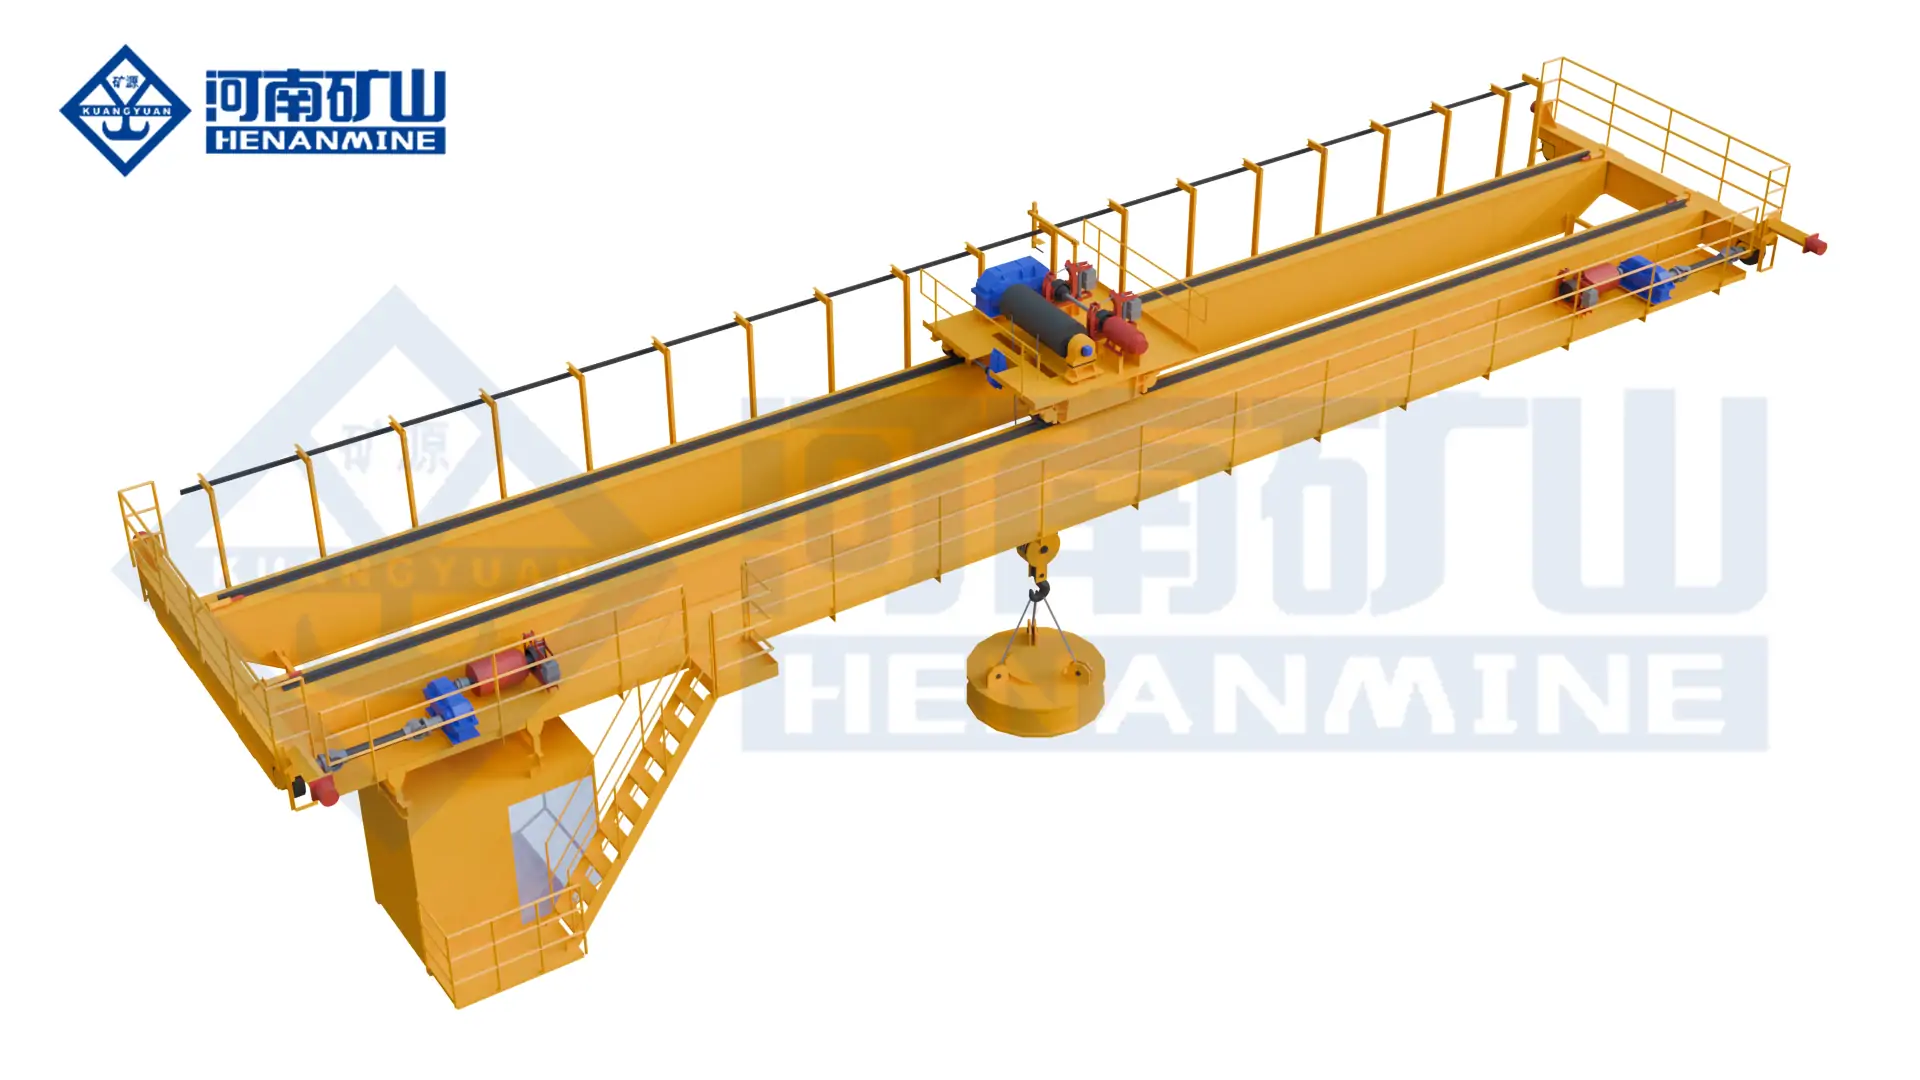
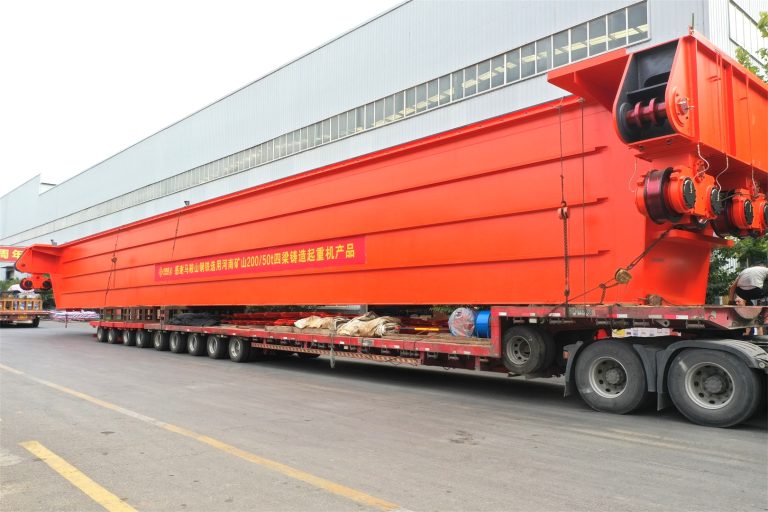
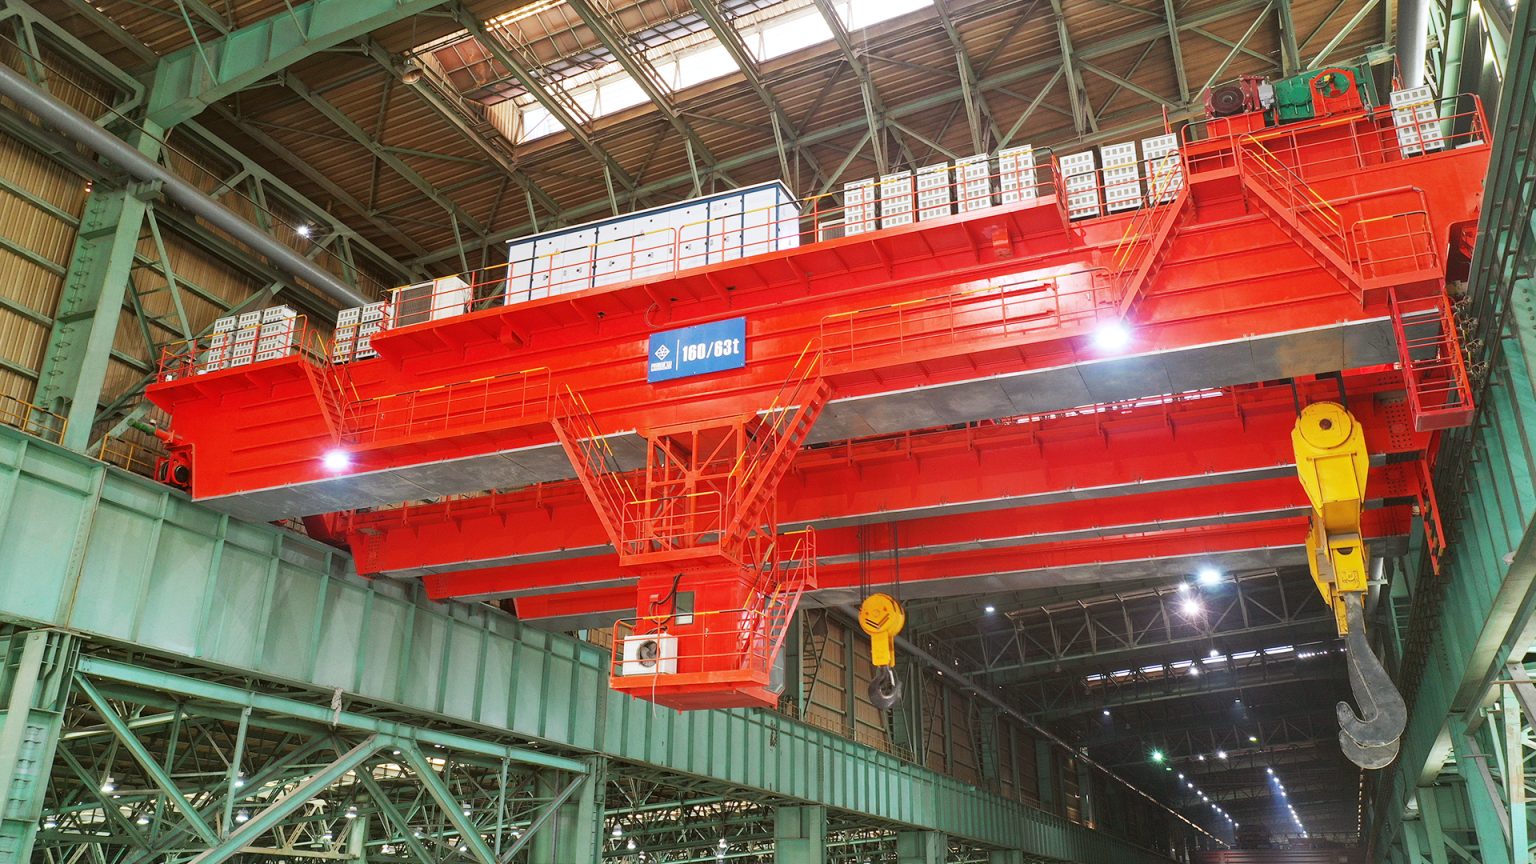
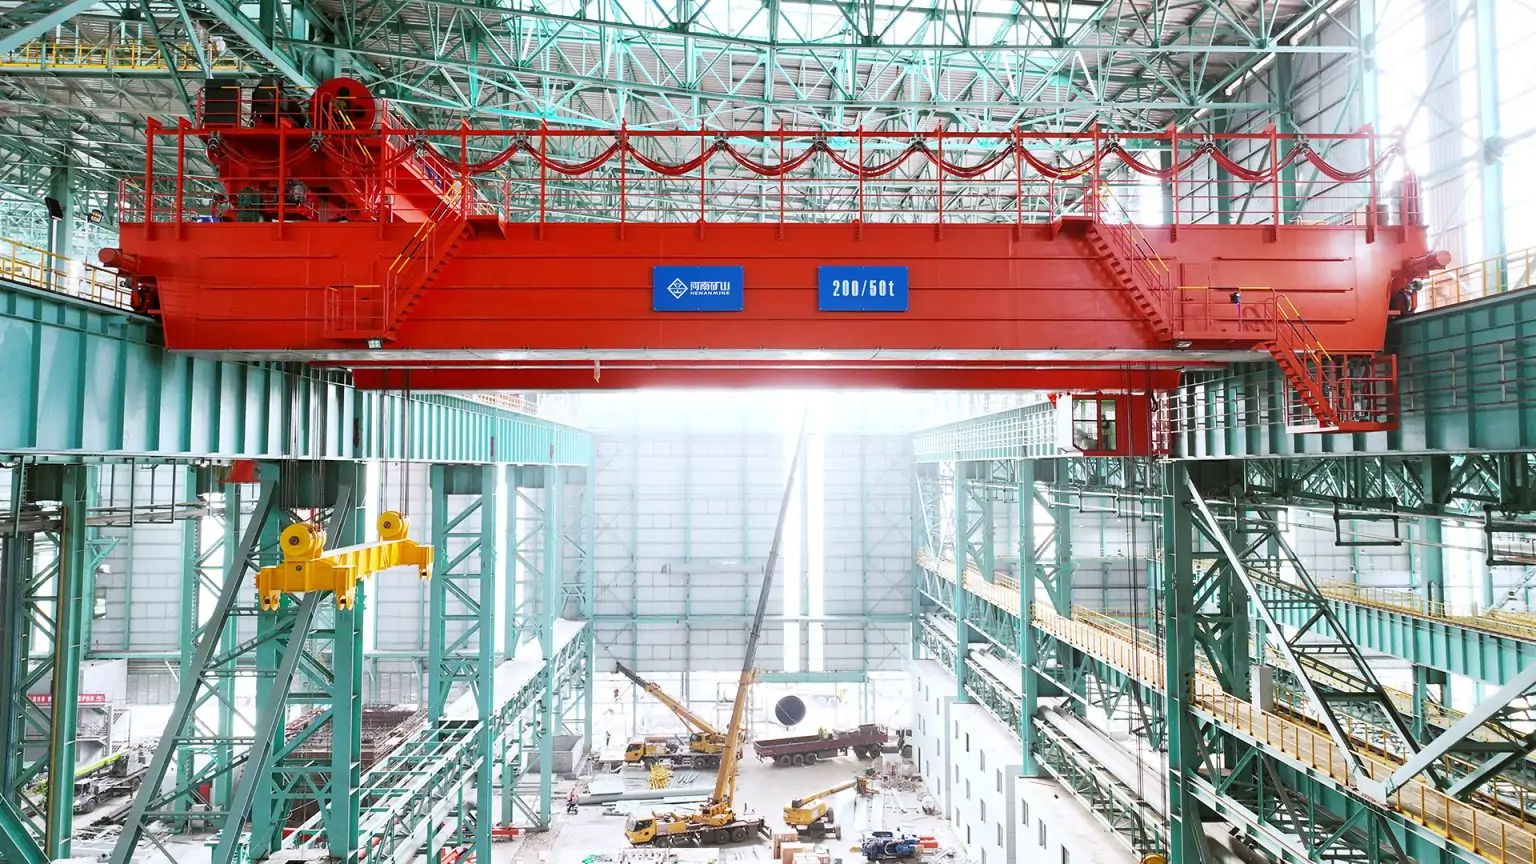
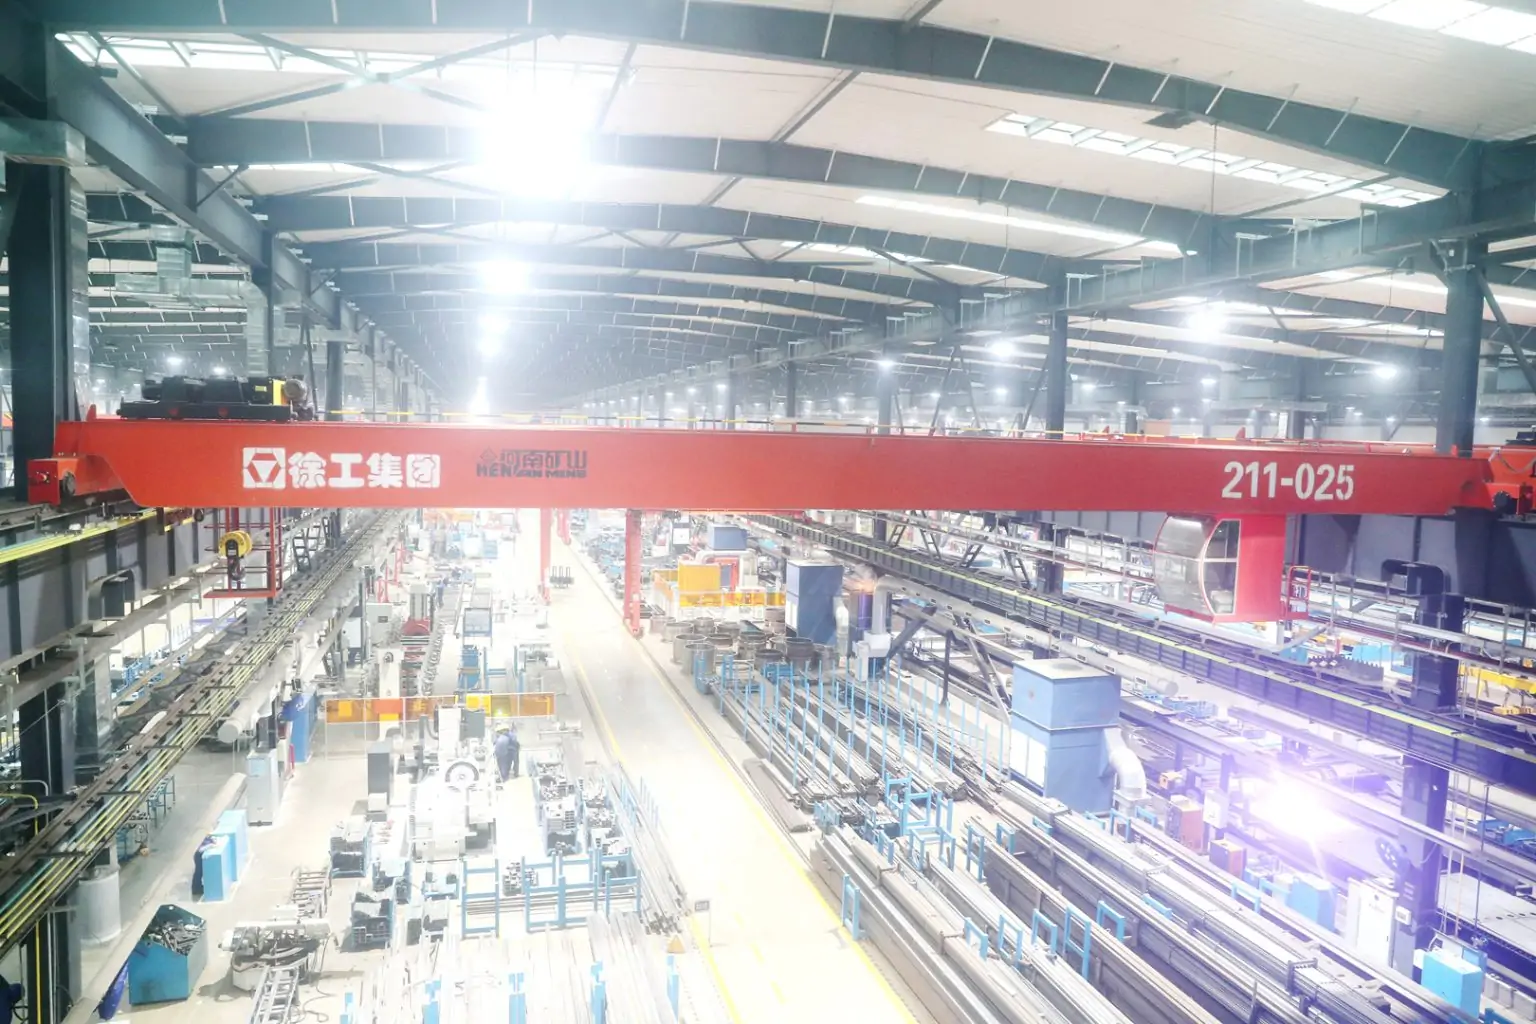
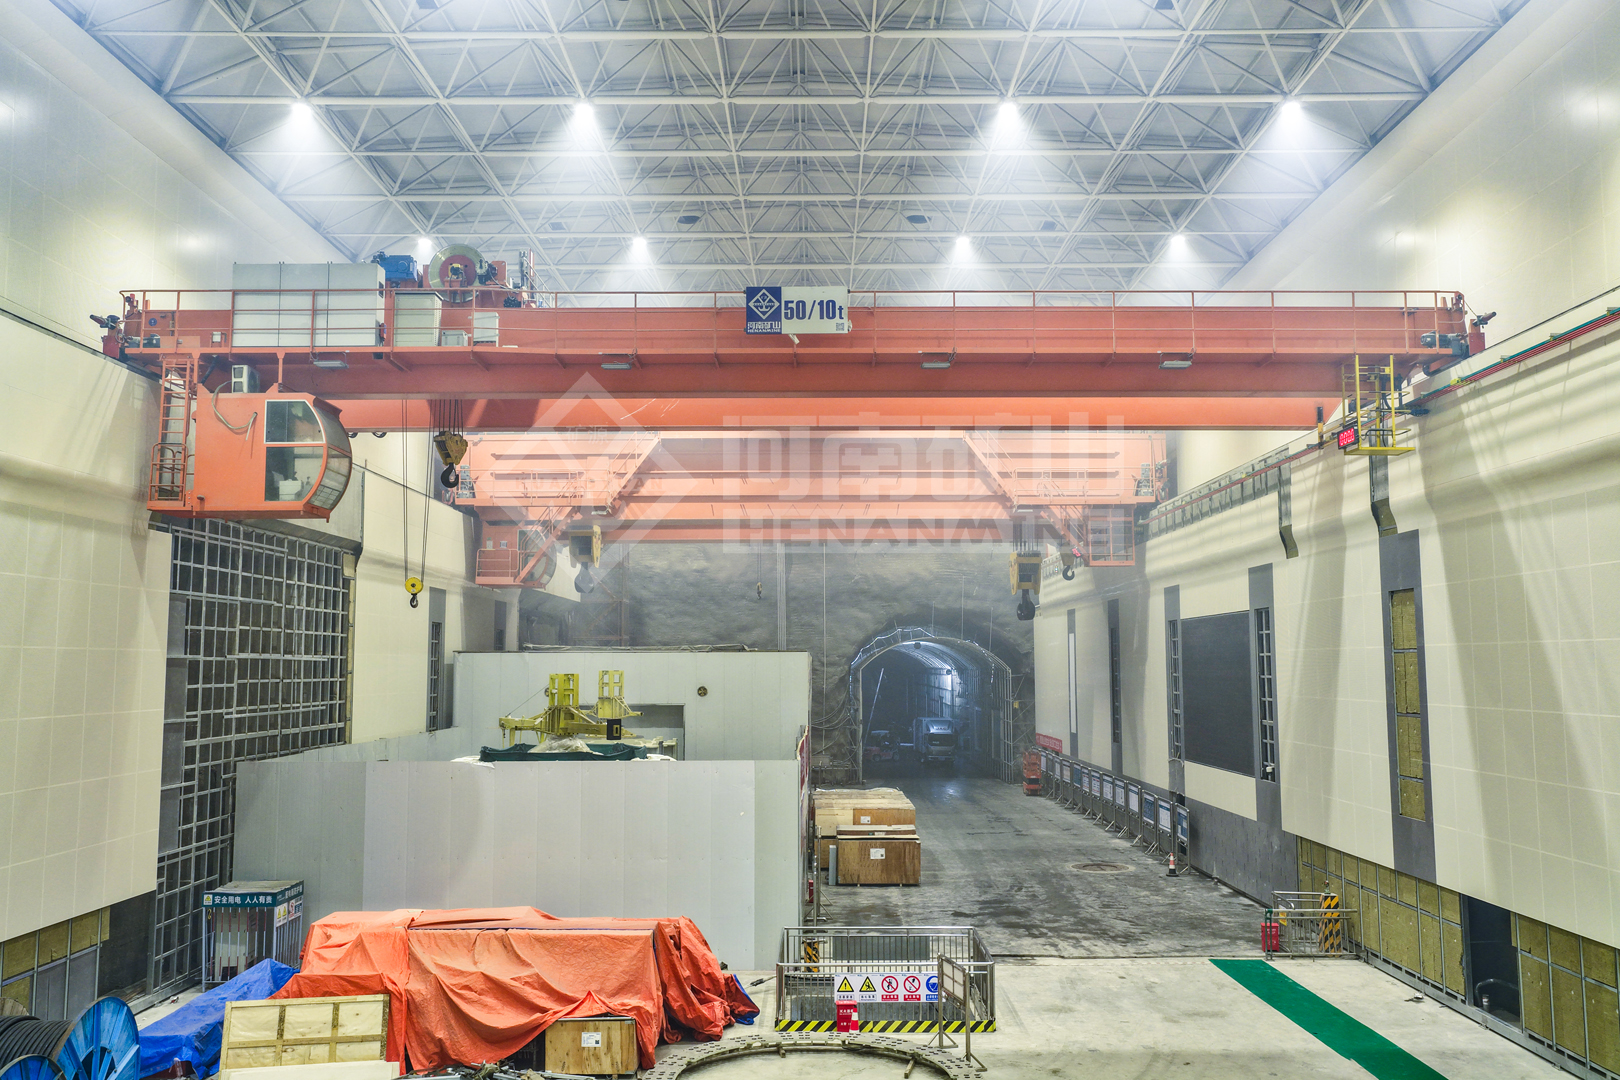
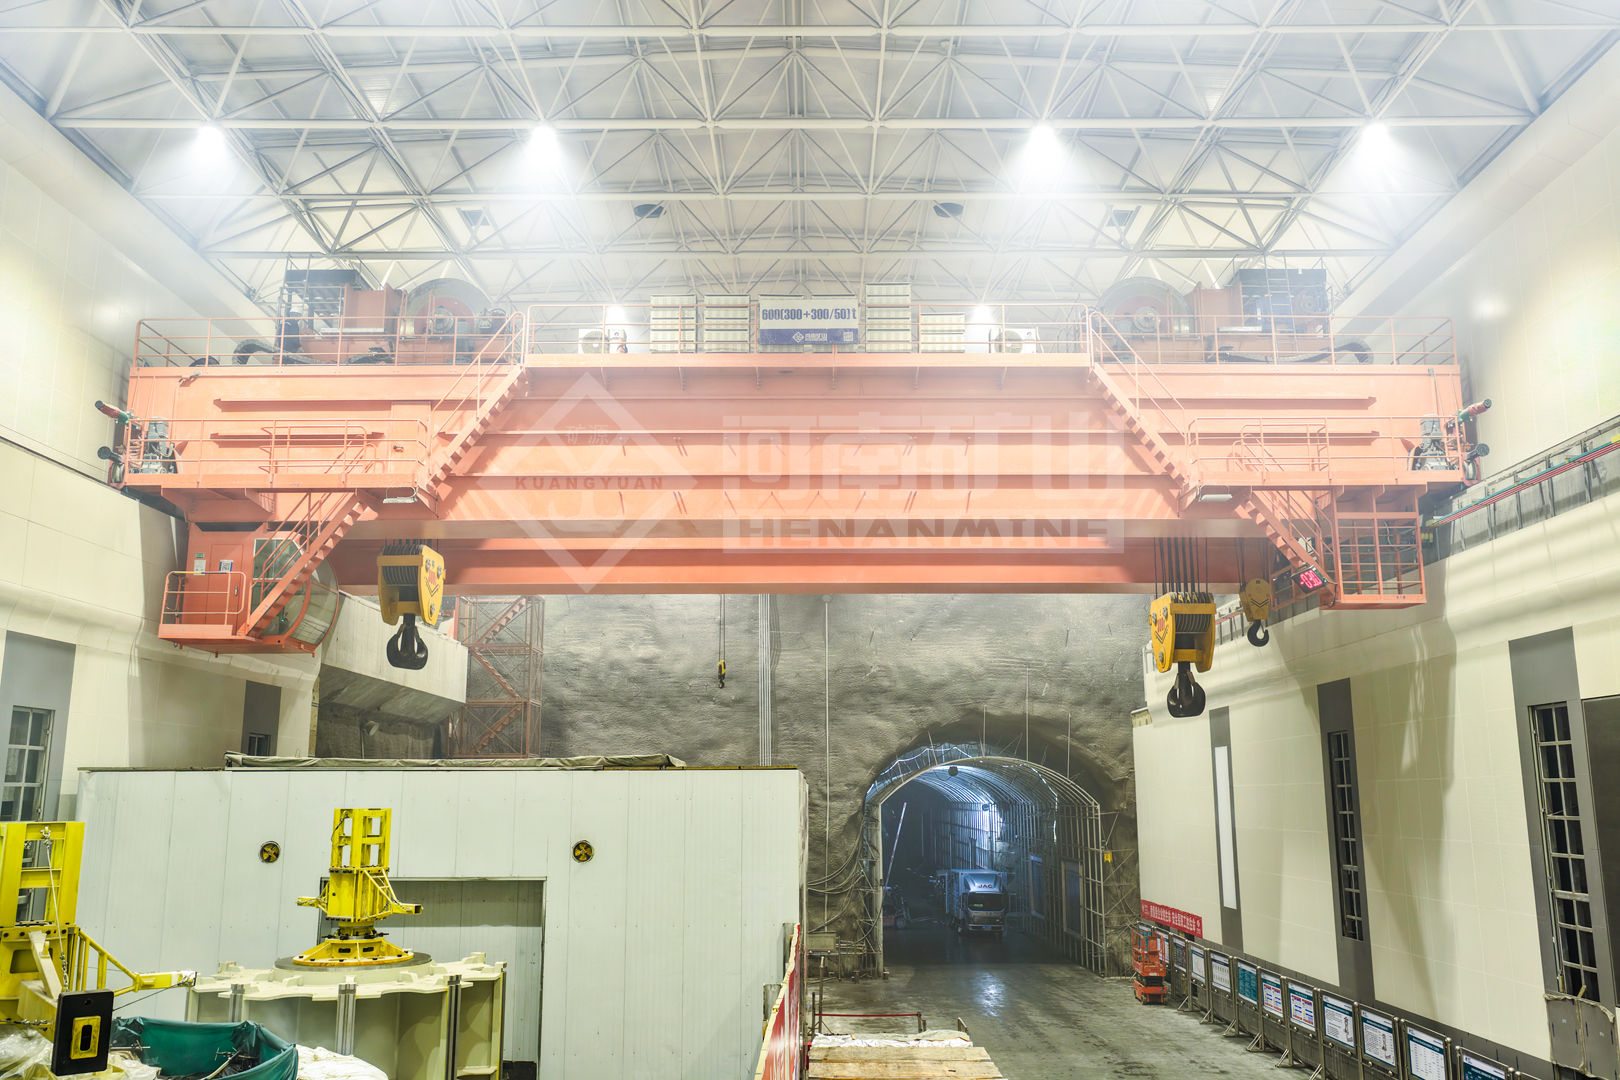
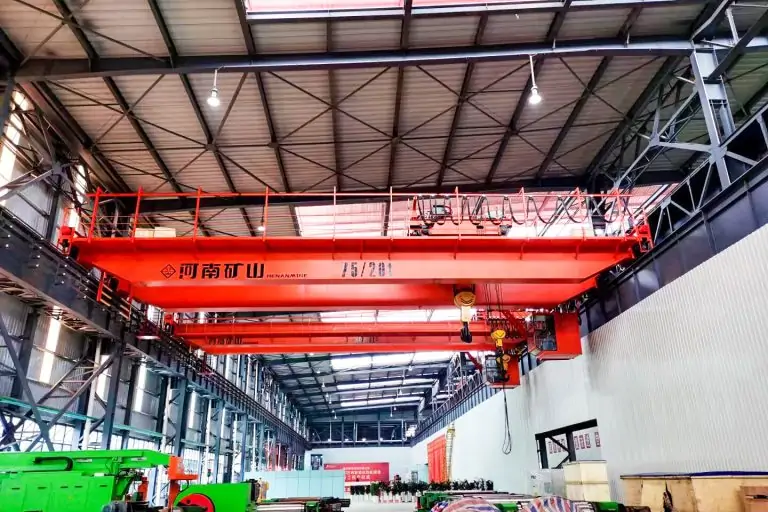
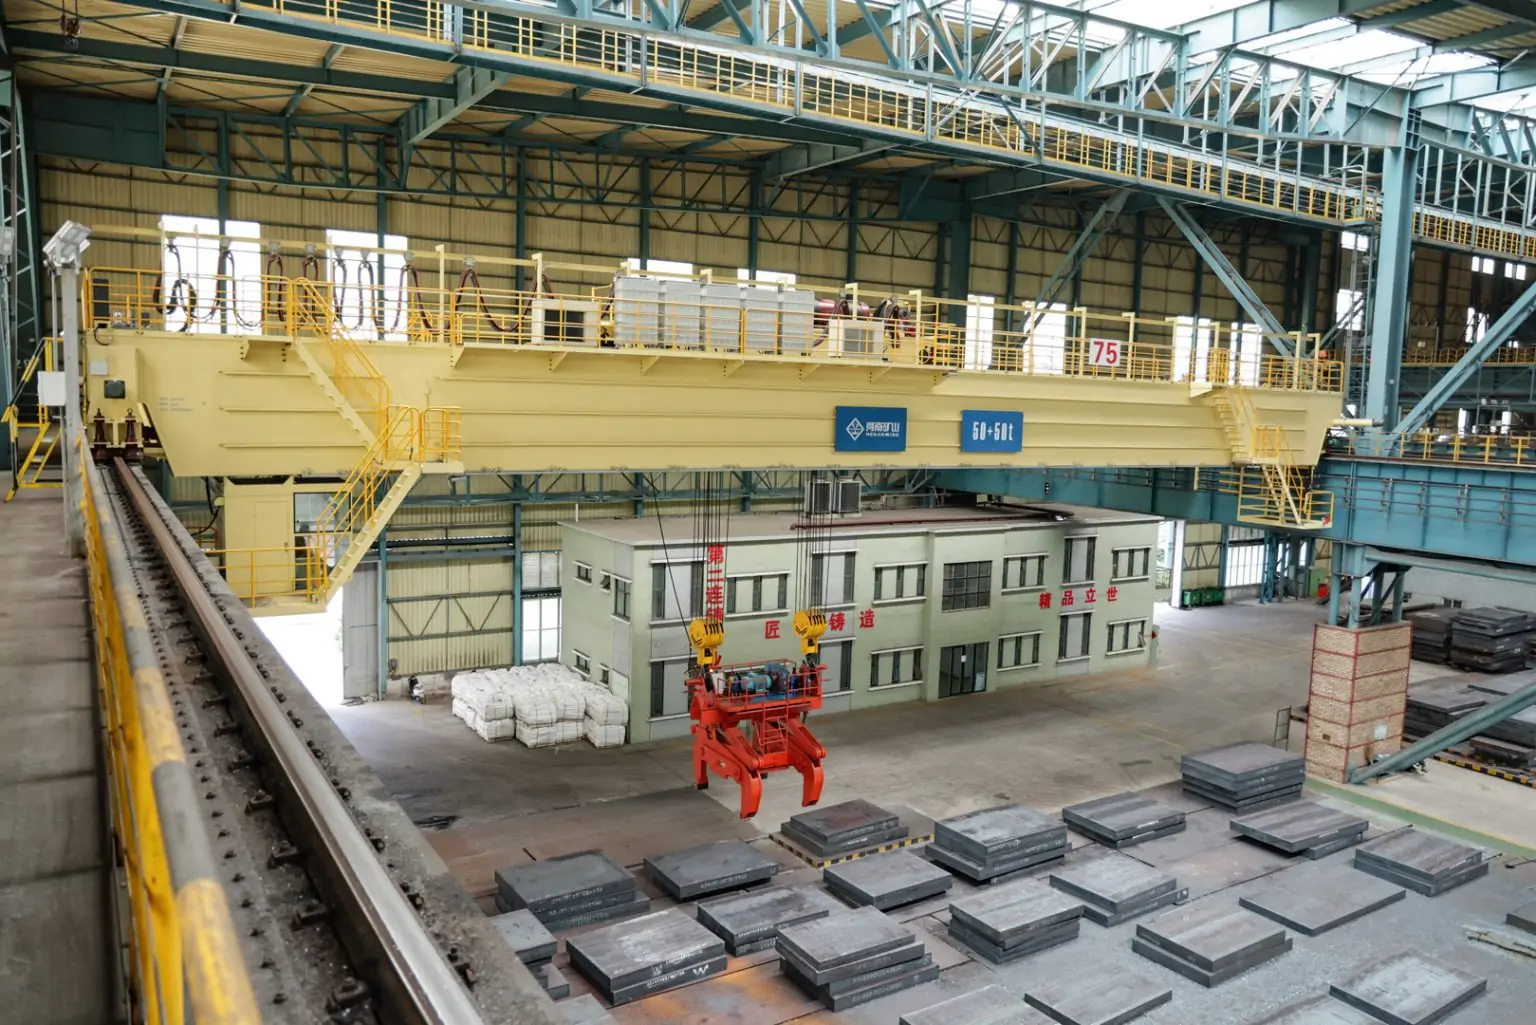
    heavy-duty double-girder metallurgical crane platform for a custom forging crane system
    A forging crane is engineered around the actual press-shop load path, including the workpiece, tongs or turning device, hook blocks and every suspended accessory.

    PRIMARY STRUCTURE

    Heavy-Duty Double Girder

    PROCESS LOADS

    Hot Ingots, Dies & Forgings

    HANDLING METHODS

    Hooks, Tongs, Clamps & Turners

    CONTROL OPTIONS

    Cabin, Radio, PLC & Automation

    What Is a Forging Crane?

    A forging crane, also called a forge-shop crane or forging overhead crane, is a process crane built for the thermal, mechanical and production demands of a forging facility. It moves hot or cold stock between furnaces, presses, hammers, manipulators, inspection stations, heat-treatment equipment and storage positions. A specialized system can also rotate or reposition a workpiece during the forging sequence.

    The term covers two substantially different duties. A forge-shop handling crane transfers ingots, dies, tooling and finished forgings between stations. A press-coordinated forging crane participates directly in open-die forging by supporting and turning a heavy workpiece in coordination with the press or manipulator. The second duty normally requires higher working intensity, controlled load buffering, purpose-designed turning equipment and a control philosophy matched to the production sequence.

    A forging crane is not automatically a foundry crane. Foundry or casting cranes are designed for ladles and molten metal; quenching cranes are designed for rapid immersion into a treatment bath. Either may be required elsewhere in the same plant, but each process must be specified separately. Henan Mine Crane develops the forging system from the declared solid-workpiece duty and integrates relevant features from its metallurgical bridge crane and double-girder bridge crane platforms.

    Forging Crane Applications

    Open-Die Forging Press

    Support, rotate and reposition large ingots or forgings through repeated press strokes using approved hooks, tongs or a powered turning device.

    Forging Hammer Bay

    Transfer heated stock, dies and tooling while accounting for shock, vibration, scale and restricted approach around the hammer foundation.

    Furnace Charging and Extraction

    Move ingots or billets to and from heating furnaces with attachment clearance, radiant-heat protection and a controlled pickup orientation.

    Die and Tool Handling

    Change upper and lower dies, anvils, saddles and press tooling with the hook approach, creep speed and maintenance access required by the equipment layout.

    Heat Treatment and Cooling

    Transfer forged parts to normalizing, annealing, cooling or inspection positions; rapid immersion requires a separately defined quenching-crane function.

    Machining and Dispatch

    Move cooled forgings between cleaning, inspection, machining, weighing, storage and shipment when one crane serves the downstream production route.

    Components and Operating Principle

    1. Bridge and end carriages: carry the process trolley and distribute vertical, transverse and longitudinal reactions to the runway.
    2. Main hoist: supports the maximum forging, ingot, die or suspended turning assembly and provides controlled lifting under the declared duty.
    3. Auxiliary hoist: supports turning, tailing, tool handling or secondary positioning when the approved operation requires two lifting points.
    4. Below-hook device: may be a hook rig, tong, clamp, spreader, chain-turning assembly or powered turning unit designed for the workpiece.
    5. Drives and controls: coordinate hoisting, trolley travel, bridge travel, creep speeds, interlocks, monitoring and optional press-line communication.
    6. Thermal and environmental protection: shields structures, ropes, cables, motors, brakes, panels, sensors and the operator station from the declared exposure.
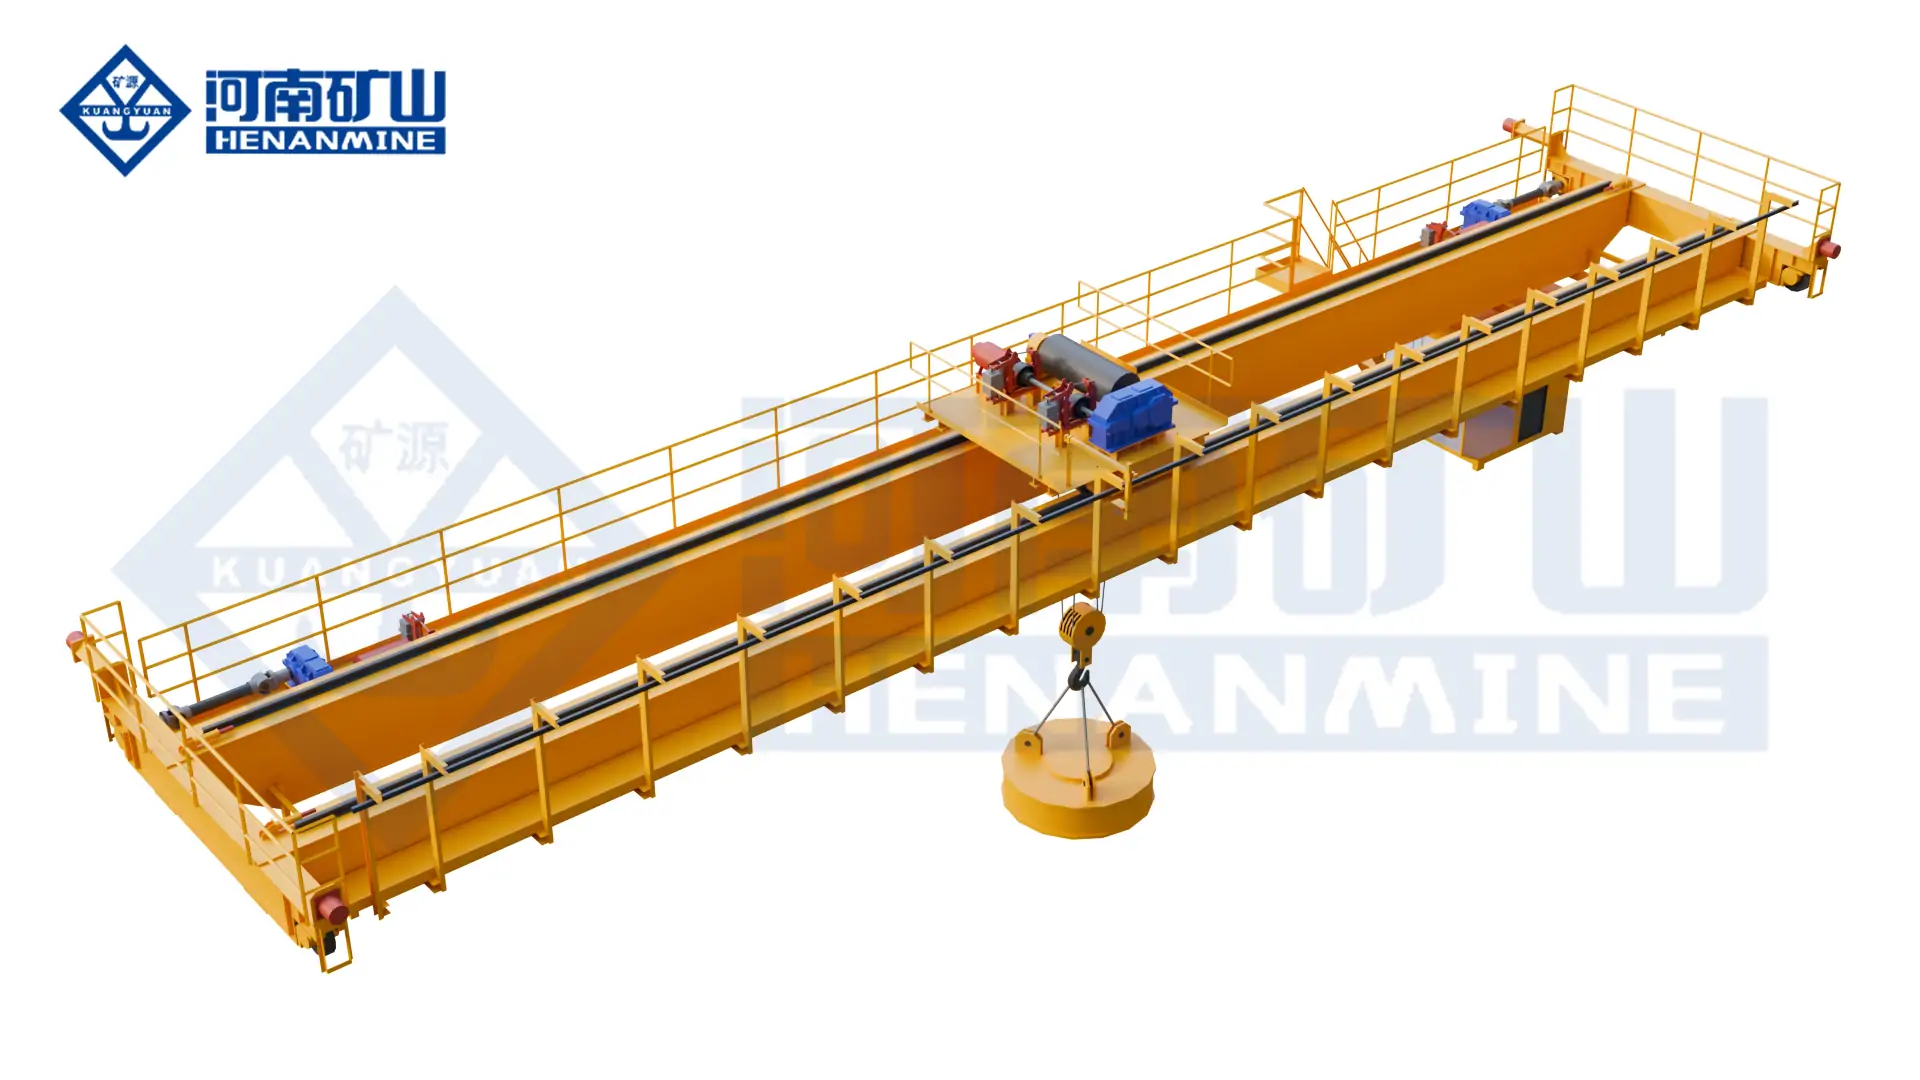
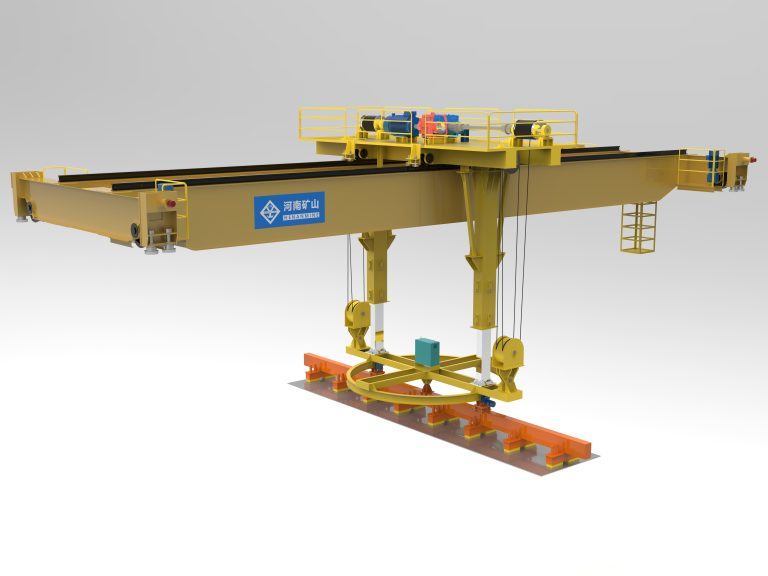
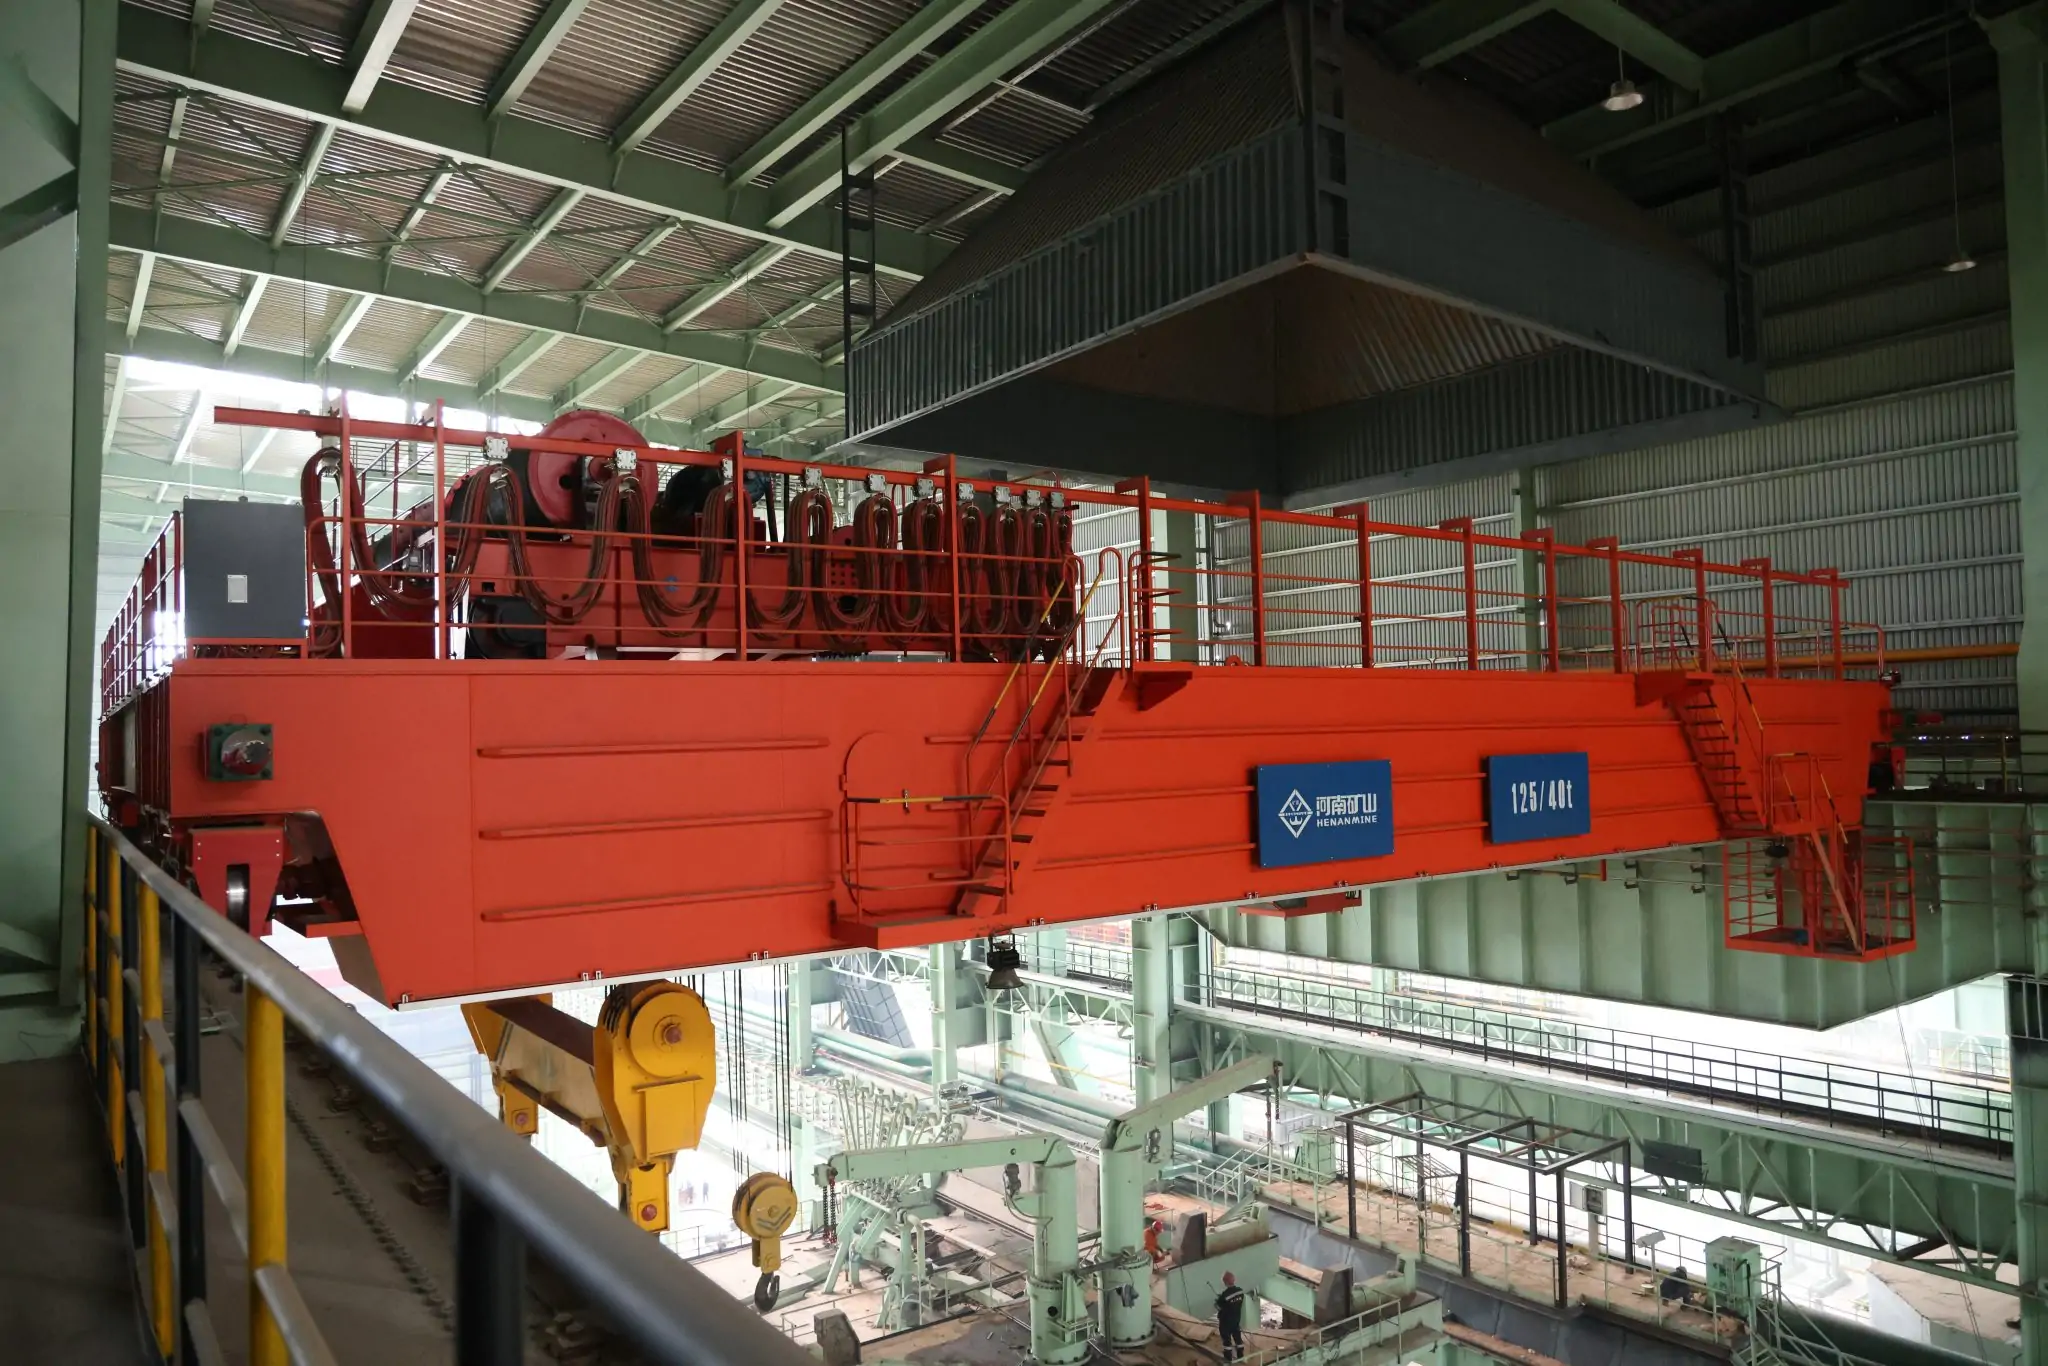
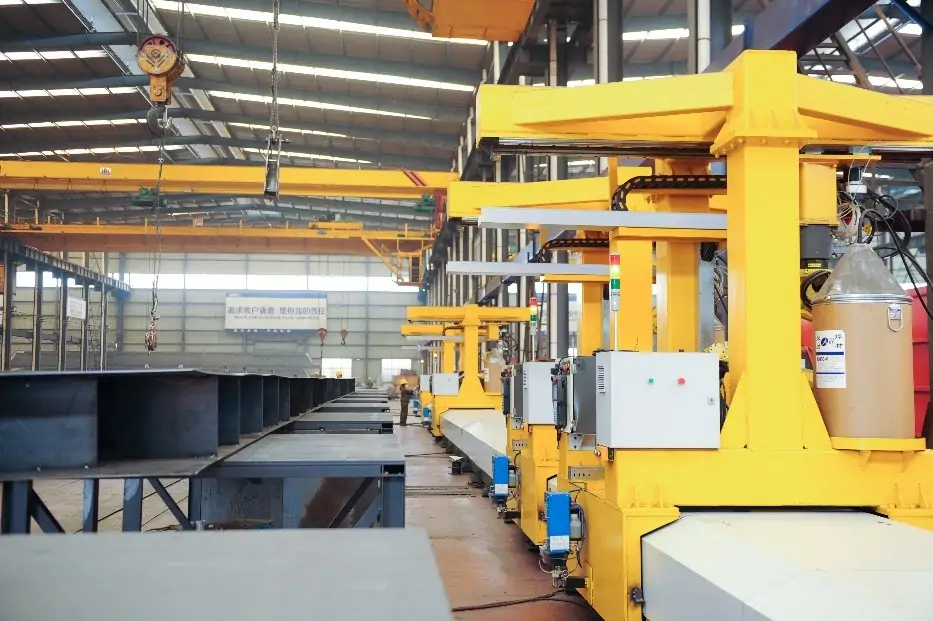
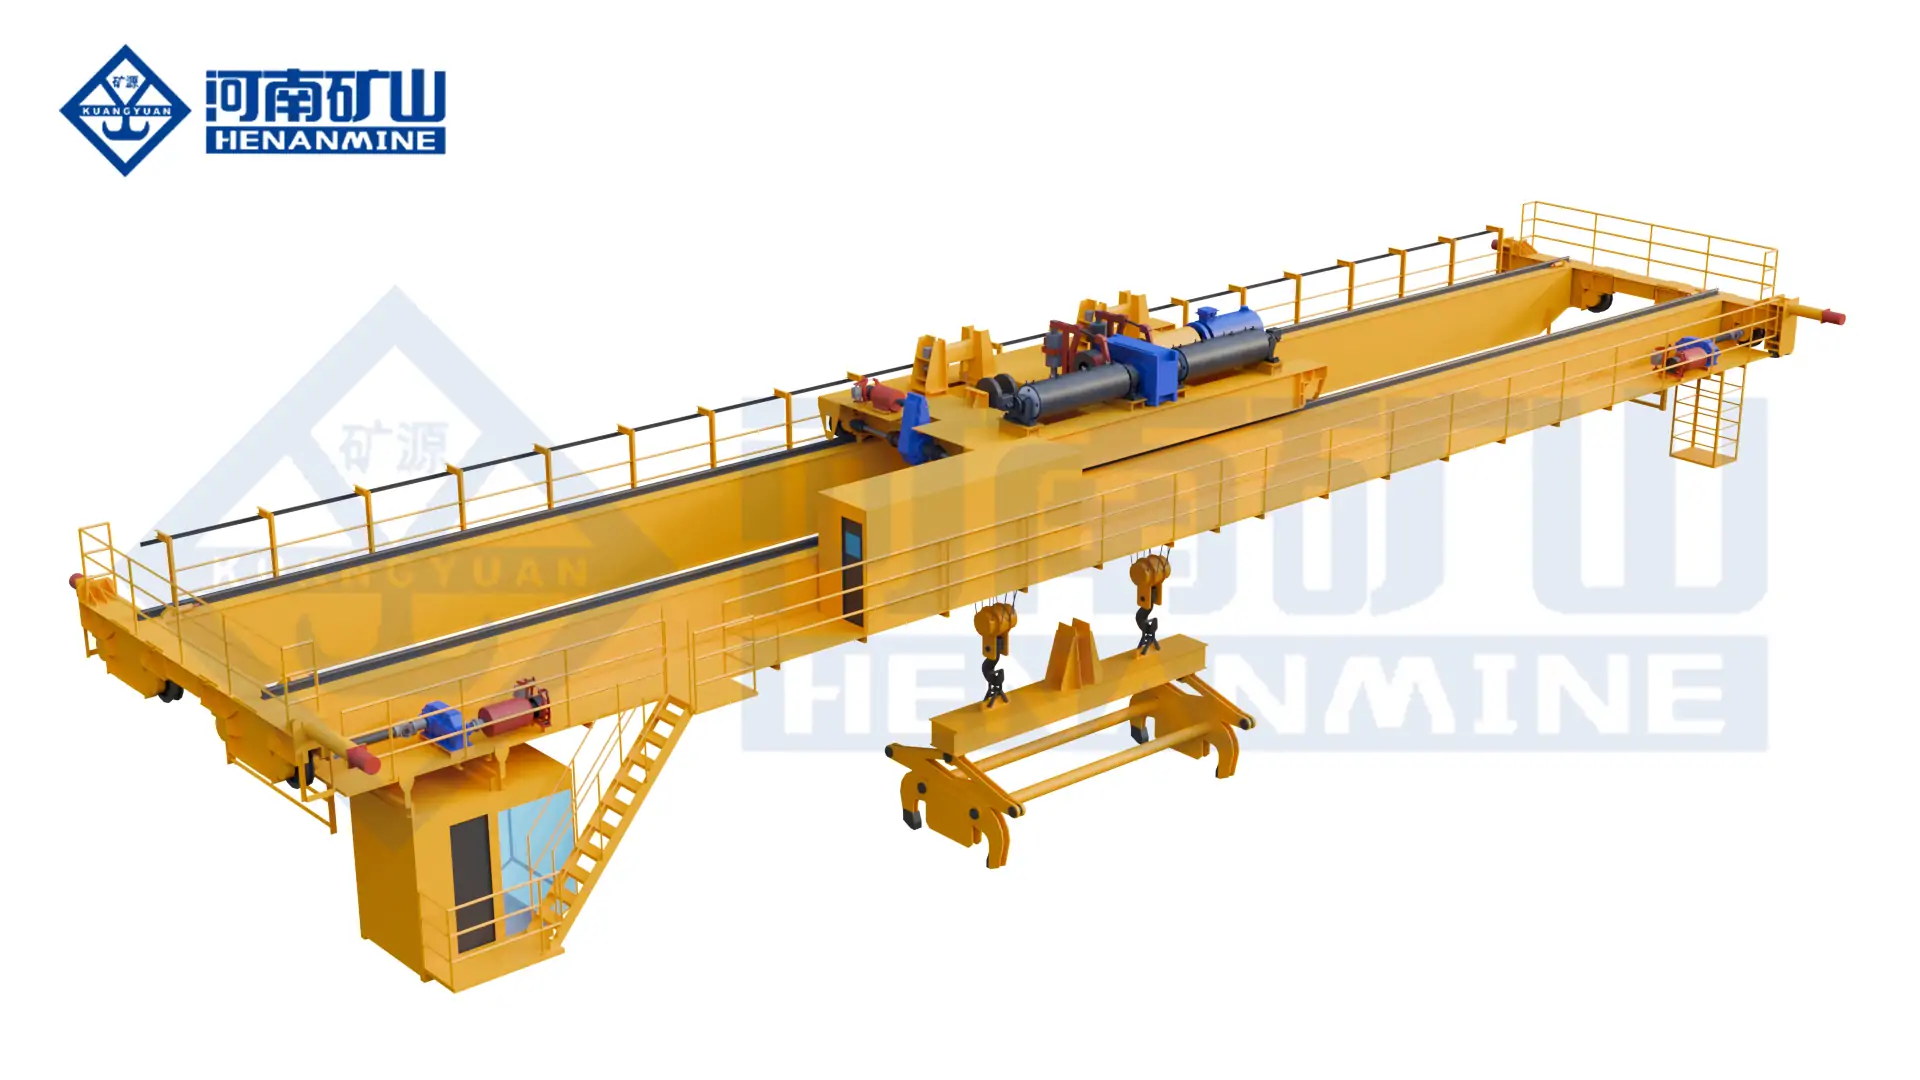
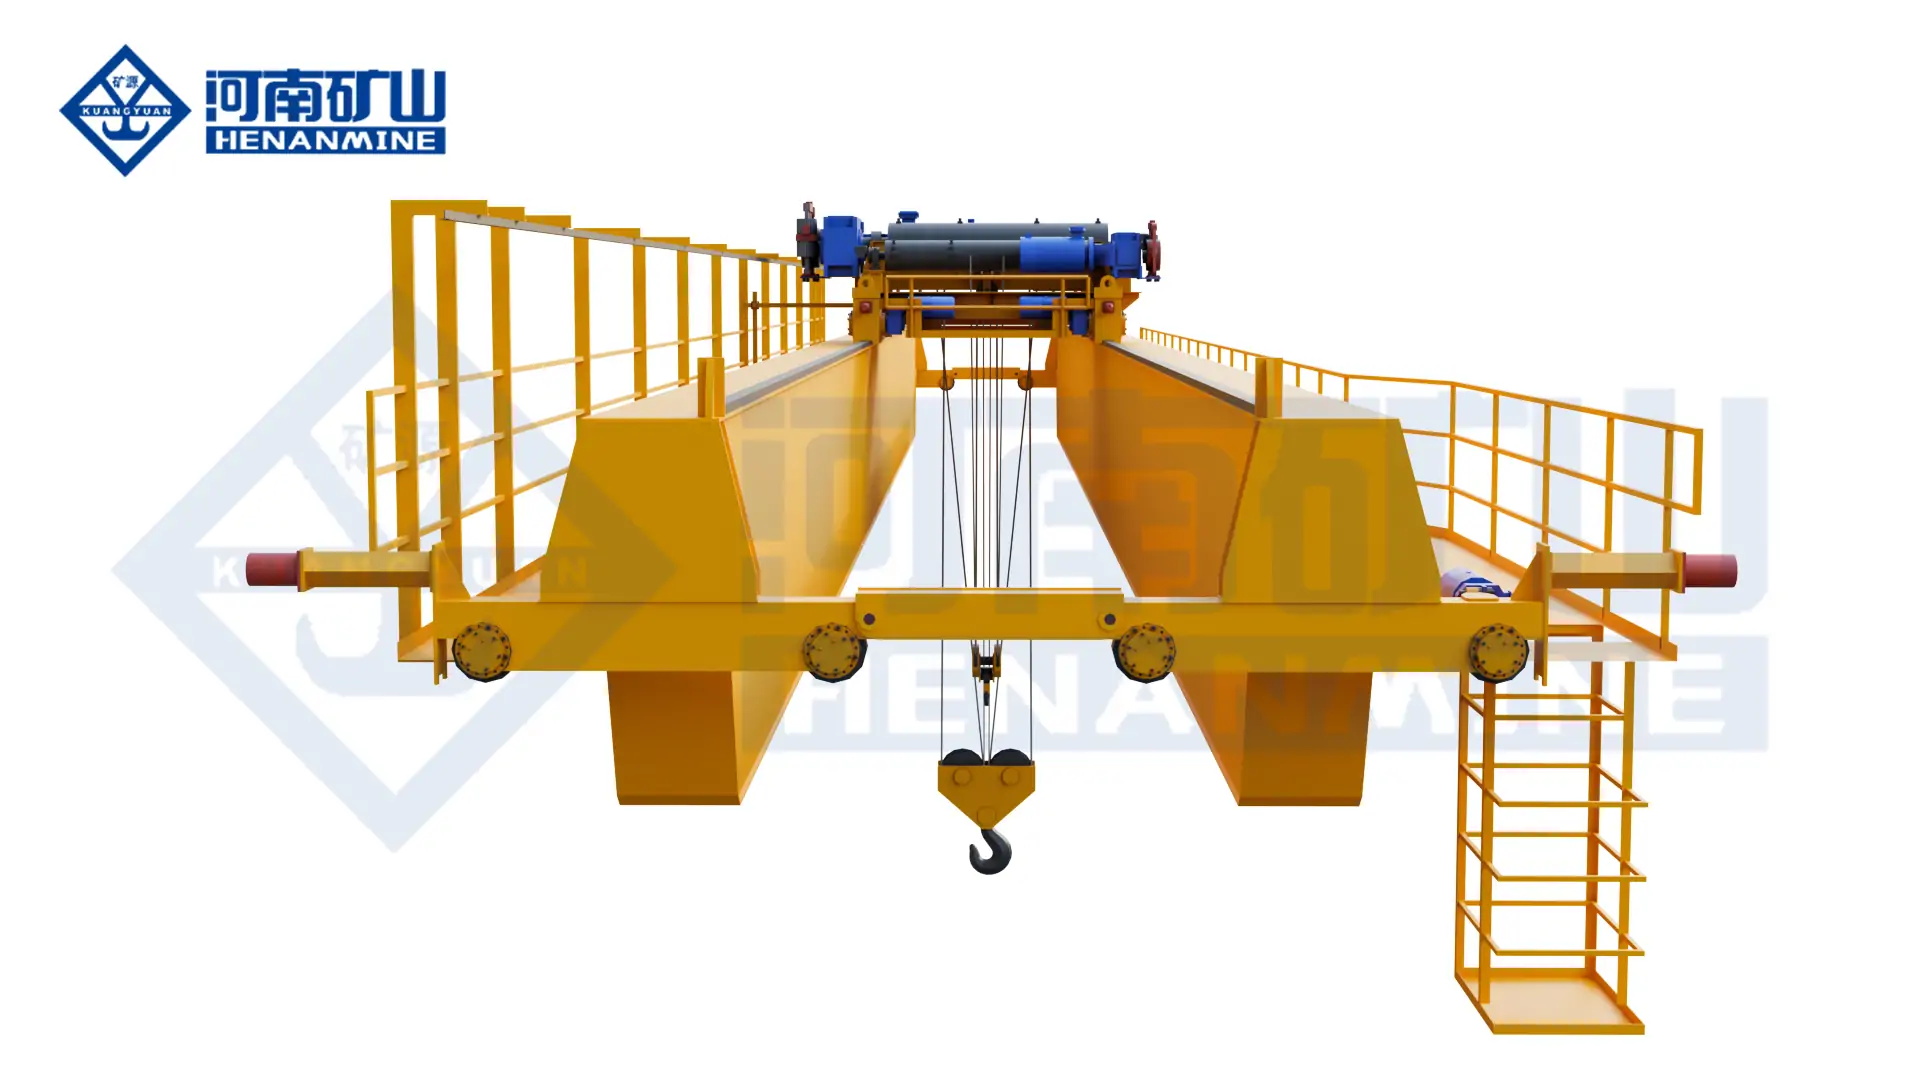
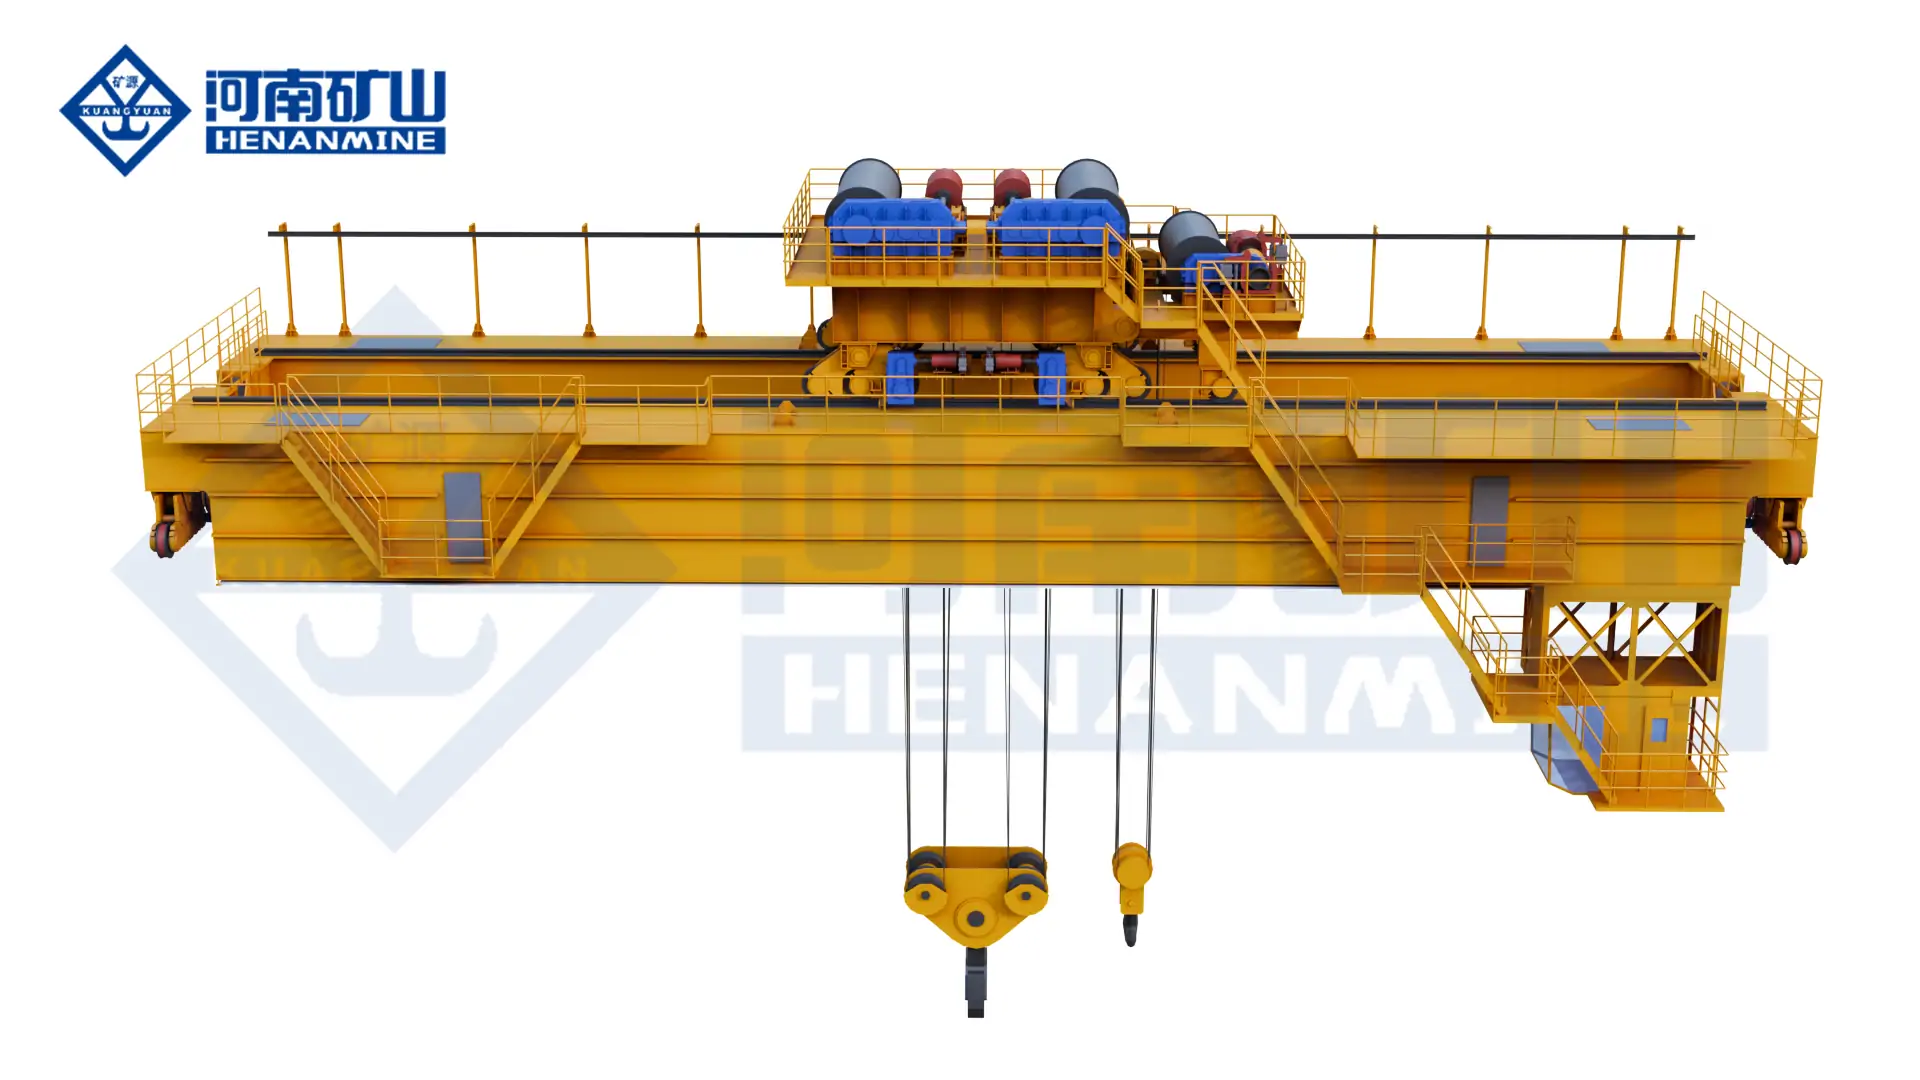
    heavy-duty metallurgical bridge crane machinery arrangement applicable to forge-shop engineering
    Bridge structure, trolley layout, reeving, brakes, ropes and thermal protection are selected as one process system rather than as isolated components.

    Rated-load basis: the crane rating starts with the maximum gross suspended load. This includes the heaviest workpiece, tongs or turning device, spreader, rigging, hook blocks and every other suspended component. The forging mass alone is not the required crane capacity.

    Forging Crane Selection Considerations

    Selection begins with the forging sequence and complete load spectrum. Nominal tonnage alone cannot define the structure, mechanisms, attachment or safety architecture.

    Load Matrix

    Minimum, typical and maximum mass; workpiece dimensions; center-of-gravity range; dies and tooling; attachment mass; single- or dual-point lifting; off-center cases.

    Forging Sequence

    Furnace pickup, press or hammer approach, rotation angle, number of turns, hold time, transfer path, handover to manipulator and downstream placement.

    Temperature and Environment

    Workpiece and furnace temperatures, radiant-heat intensity and duration, ambient range, scale, dust, smoke, oil mist, water spray, vibration and corrosive exposure.

    Duty and Dynamics

    Cycles per hour, starts and reversals, shifts, annual hours, load spectrum, press interaction, permitted shock, required buffering and production consequence of downtime.

    Building and Equipment Interface

    Rail-center span, runway length and elevation, wheel-load limits, headroom, hook approaches, press columns, furnace doors, manipulator envelope and maintenance access.

    Control and Acceptance

    Cabin or radio control, visibility, cameras, creep speed, positioning tolerance, press/MES signals, fallback modes, proof load, representative-workpiece test and documentation.
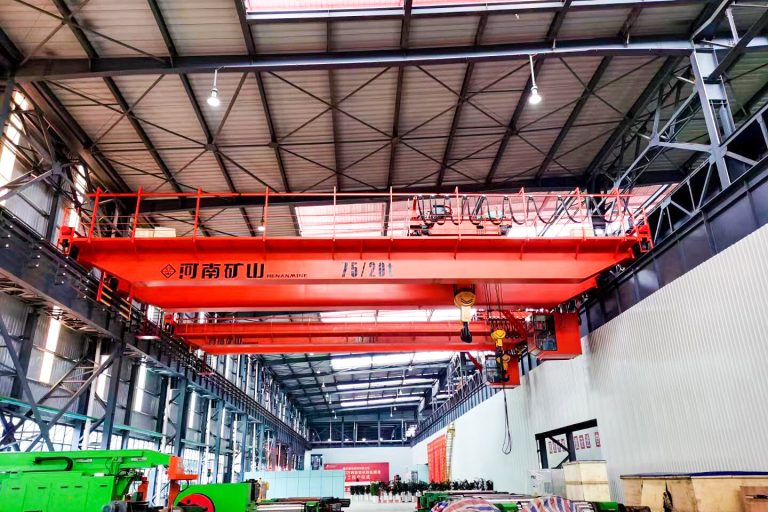
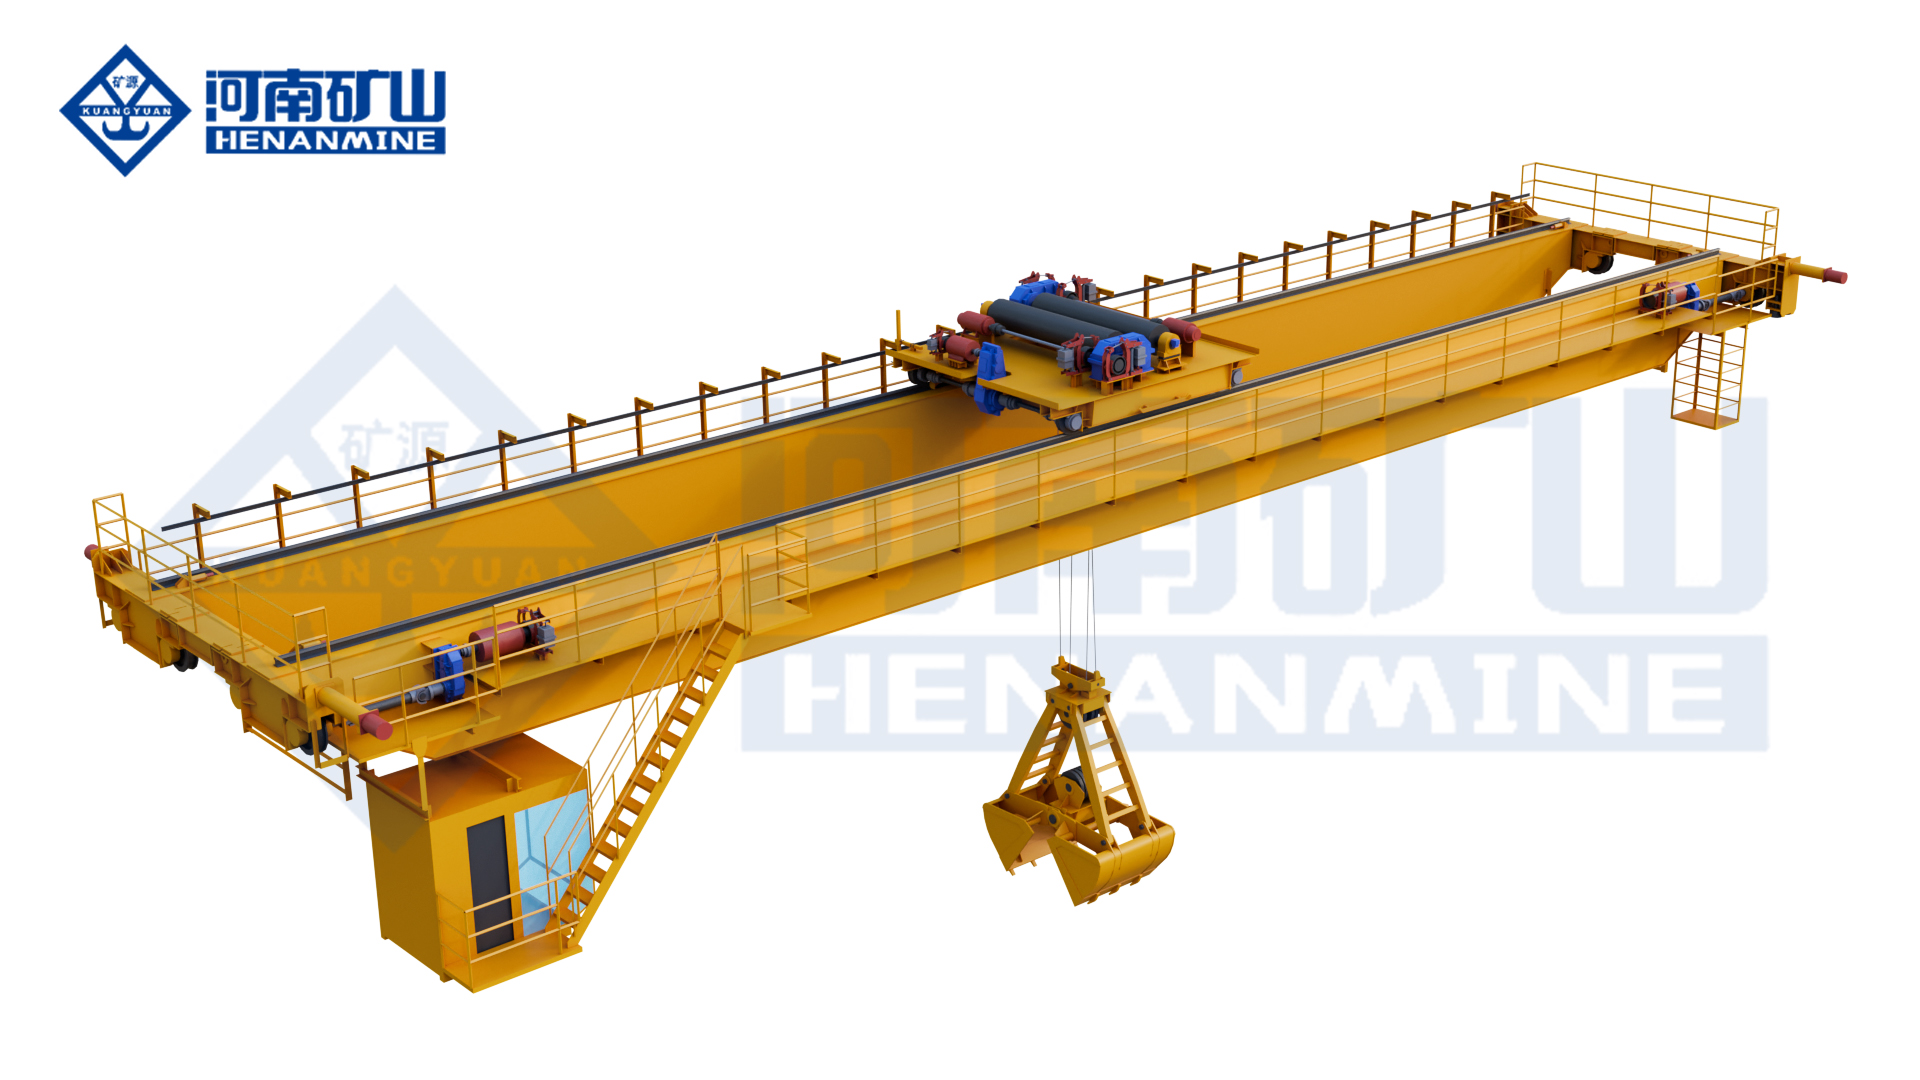
    high-temperature heavy-duty bridge crane engineering reference for forging crane selection
    The crane envelope must be checked against furnace, press, manipulator, platforms, columns, extraction systems and the full suspended-load turning radius.

    Forging Crane Configurations Compared

    The configuration follows the actual process function. Equipment from adjacent metallurgical duties should not be substituted without a complete engineering review.

    Configuration Suitable Duty Typical Load Handling Engineering Focus Selection Boundary
    Heavy-duty hook forging crane Ingot, die, tooling and forged-part transfer Main hook with approved rigging or spreader Duty, creep speed, heat protection, hook approach and maintenance access Does not provide controlled turning unless a separate system is included
    Main-and-auxiliary hook forging crane Transfer, tailing and planned load rotation Two hooks with approved turning rig or attachment Hook spacing, capacity split, synchronized control, rope fleet angles and permitted load cases The complete turning procedure must be analyzed; two hooks alone do not make every rotation safe
    Tong or clamp forging crane Repeated pickup of defined ingots, billets or forgings Mechanical, hydraulic or powered gripping attachment Grip range, surface contact, hot strength, fail-safe state, scale and attachment mass Requires a controlled workpiece range and representative validation
    Press-coordinated forging crane Direct participation in heavy open-die forging Main hoist plus turning device, tongs or manipulator interface Load buffering, impact limits, rapid reversals, positioning, communication and production availability Requires a joint functional specification with the press and manipulator supplier
    Quenching crane Rapid, controlled immersion of hot workpieces Hook, fixture or basket matched to the bath Fast lowering/lifting, emergency recovery, bath geometry, vapor and splash exposure A heat-treatment crane, not a substitute for press-coordinated forging
    Foundry or casting crane Ladle handling and molten-metal transfer Gantry hook or ladle lifting attachment Molten-metal-specific redundancy, thermal protection and regulatory requirements Required only when molten metal is in scope; it is not the standard crane for solid forgings

    Preliminary Forging Crane Specification Framework

    The values below identify the decisions required for a technical proposal. Final parameters are established after the load cases, process sequence and workshop interfaces are approved.

    Parameter Project Definition Required Input
    Rated lifting capacity Selected from maximum gross suspended load and governing load cases Workpiece, attachment, rigging, hook block and off-center loads
    Main / auxiliary capacity Single hoist, main plus auxiliary, or coordinated multi-hoist arrangement Turning method, capacity split and simultaneous-use cases
    Structure and trolley Double-girder process crane; special multi-girder or dual-trolley layout where justified Capacity, span, wheel loads, headroom, rigidity and access
    Span and lifting height Engineered from rail centers, hook travel and process clearance Workshop section, press/furnace drawings and runway survey
    Working duty Calculated under the selected classification system Load spectrum, cycles, starts, shifts, annual hours and process dynamics
    Hoisting and travel speeds Process, transfer and creep speeds with variable-frequency control as required Cycle time, positioning tolerance, travel distance and load stability
    Thermal design Heat shields, protected components, cooling or relocated equipment Workpiece temperature, radiant flux or distance/time profile and ambient range
    Control system Cabin, radio, local station, semi-automatic or integrated automatic control Visibility, operator location, interfaces, fallback mode and safety zones
    Power and environment Matched to destination voltage, frequency, enclosure and protection requirements Site power, dust, scale, smoke, humidity, altitude and corrosion
    Compliance route One coherent contractual design and inspection basis Destination, local authority, purchaser specification and required certification

    Market envelope: specialized suppliers publicly present dedicated heavy forging cranes in approximately 180–550 t capacities, 24–33 m spans and 17–28 m lifts. Smaller forge-shop handling cranes and larger custom systems also exist. These are market reference ranges, not fixed Henan Mine Crane catalog limits or a substitute for project calculations.

    Hot-Workpiece Handling and Turning Engineering

    Turning a forging creates load cases that may be more demanding than a straight vertical lift. The center of gravity moves, sling or chain angles change, one hook can temporarily carry a larger share, and the workpiece may contact a saddle, manipulator or die. The approved method must define the load path through every stage.

    Main + Auxiliary Hooks

    Define simultaneous-use capacity, hook spacing, permitted angles, speed coordination and the maximum reaction on either hoist.

    Powered Turning Device

    Specify torque, workpiece range, rotation speed, restraint, heat protection, emergency state and attachment-to-crane interface.

    Tongs and Clamps

    Validate grip range, hot material behavior, contact pressure, surface scale, loss-of-power condition and visual confirmation.

    Rigging and Saddles

    Confirm temperature rating, bend radius, edge protection, contact geometry, inspection access and storage away from radiant heat.
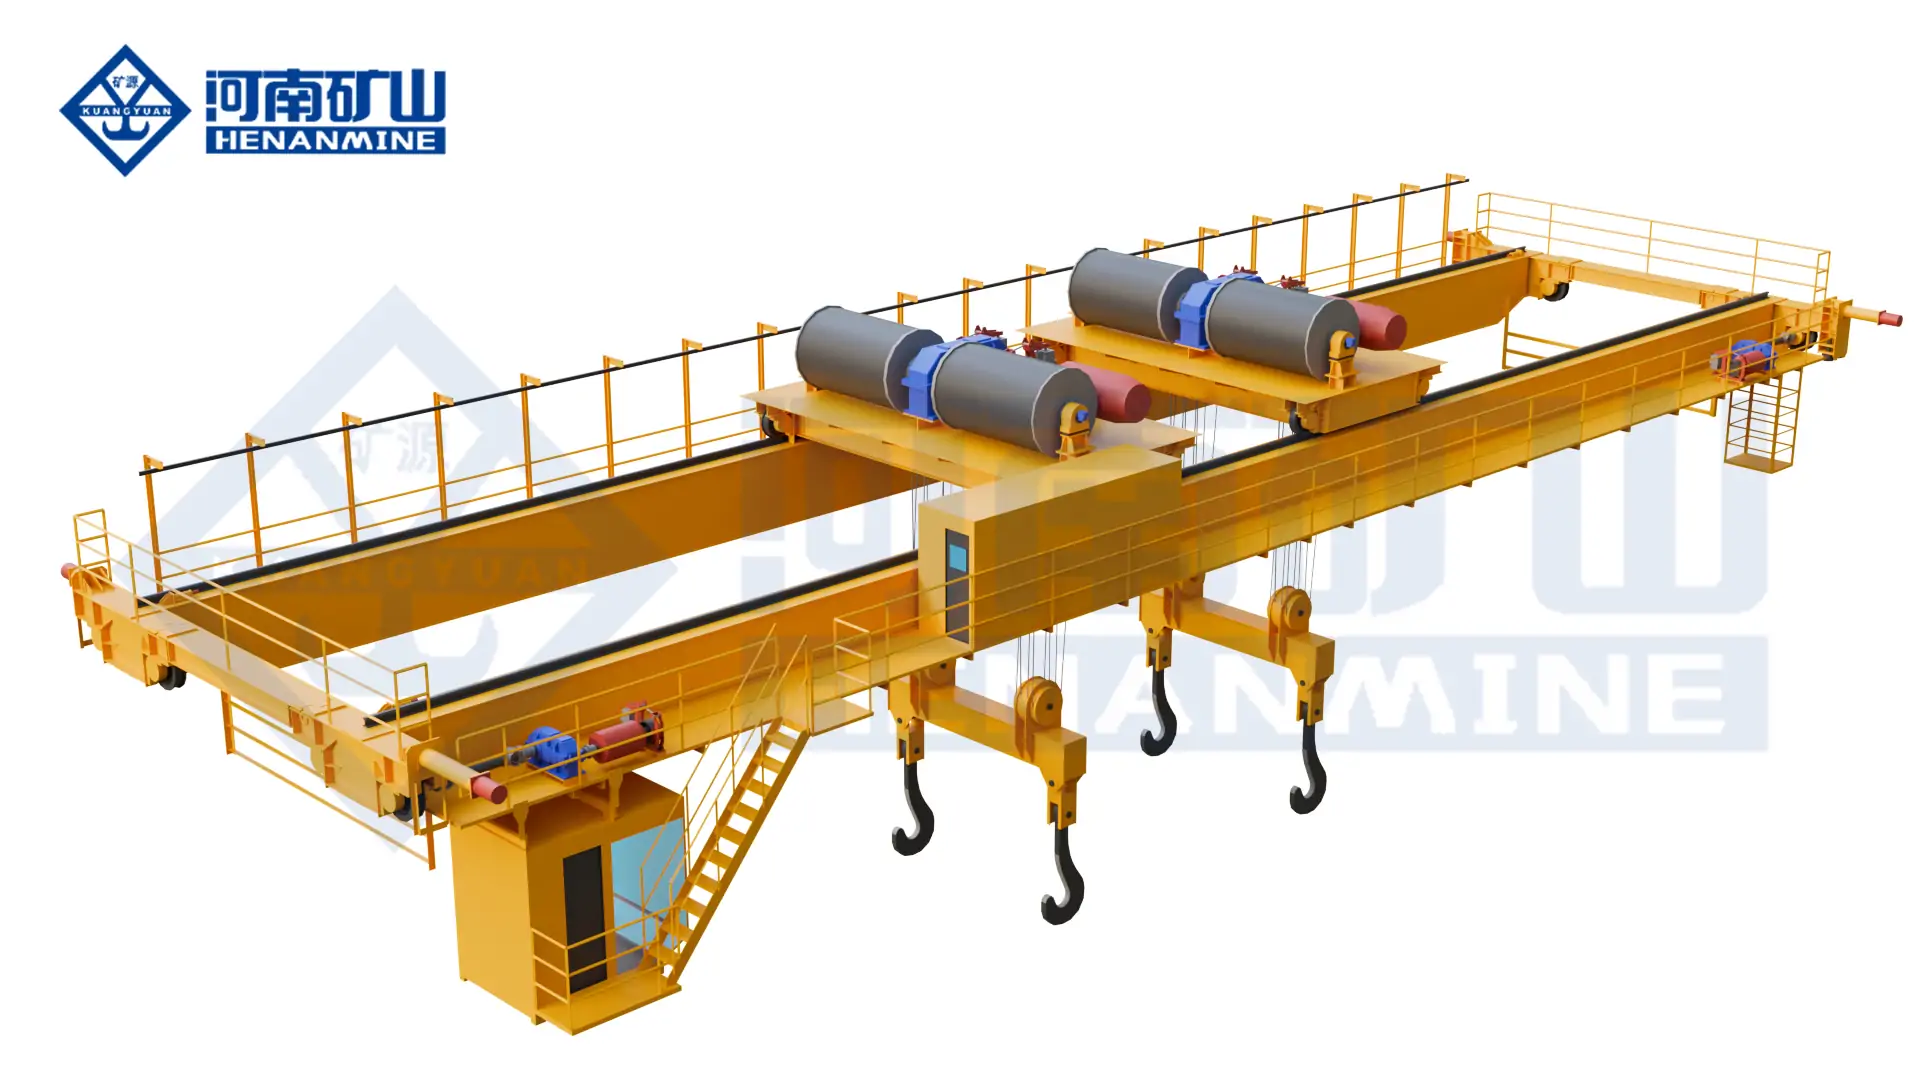
    metallurgical material turnover crane platform for controlled hot forging rotation
    A turning system is defined by the workpiece matrix, required rotation, temperature, attachment geometry and the most highly loaded point in the sequence.

    Process control: no operator should have to improvise the turning sequence. The approved lifting plan, control logic, permissible load cases, communication signals and abnormal-condition recovery are established before commissioning and verified with representative loads.

    Heat, Scale, Shock and Environmental Protection

    Thermal Mapping

    Evaluate workpiece temperature, exposure distance, dwell time and radiant paths at the hooks, trolley, girders, cabin, panels and maintenance platforms.

    Protected Hoisting System

    Select ropes, drums, sheaves, bearings, lubrication, brakes and cables for the measured environment and shield them from direct heat and scale.

    Electrical Protection

    Use suitable enclosures, cable routing, cooling or equipment relocation and monitor critical temperatures where the risk assessment requires it.

    Shock and Vibration

    Define permitted process forces, acceleration limits, buffering and structural fatigue cases; the crane must not be used to absorb undefined press or hammer impacts.

    Operator Visibility

    Coordinate cabin position, heat-resistant glazing where specified, cameras, lighting, audio communication and safe radio-control locations.

    Maintainability

    Provide safe access to brakes, ropes, sheaves, drives, panels and attachment points, with guards and shields removable under an isolation procedure.
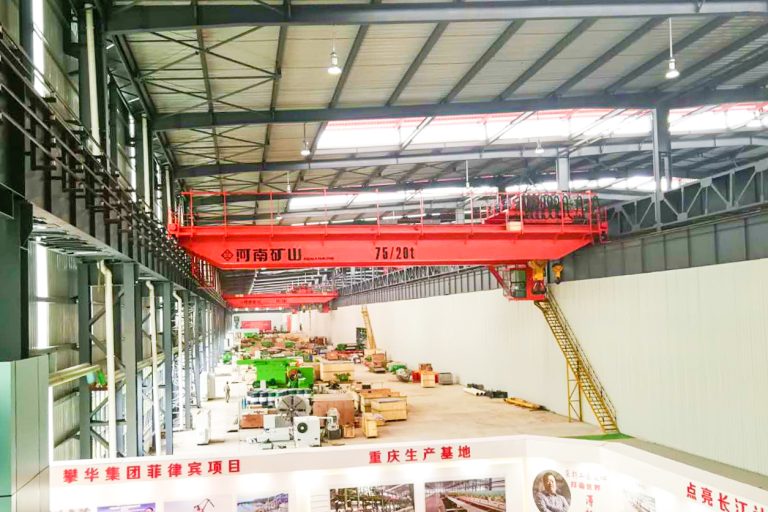
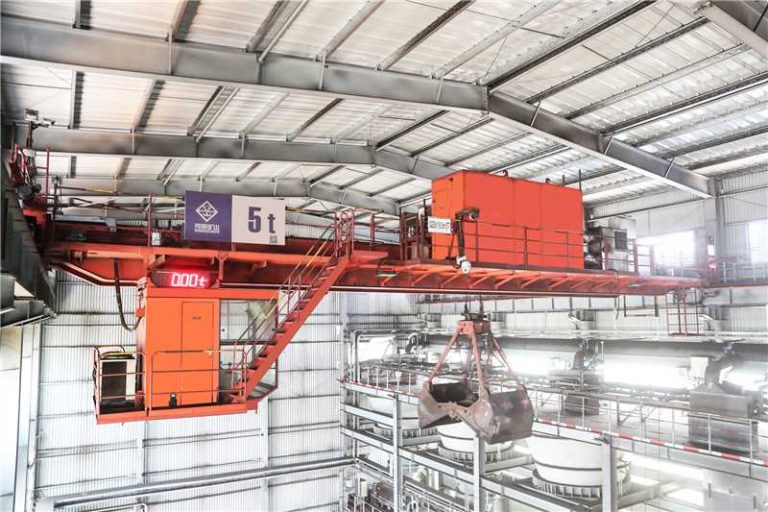
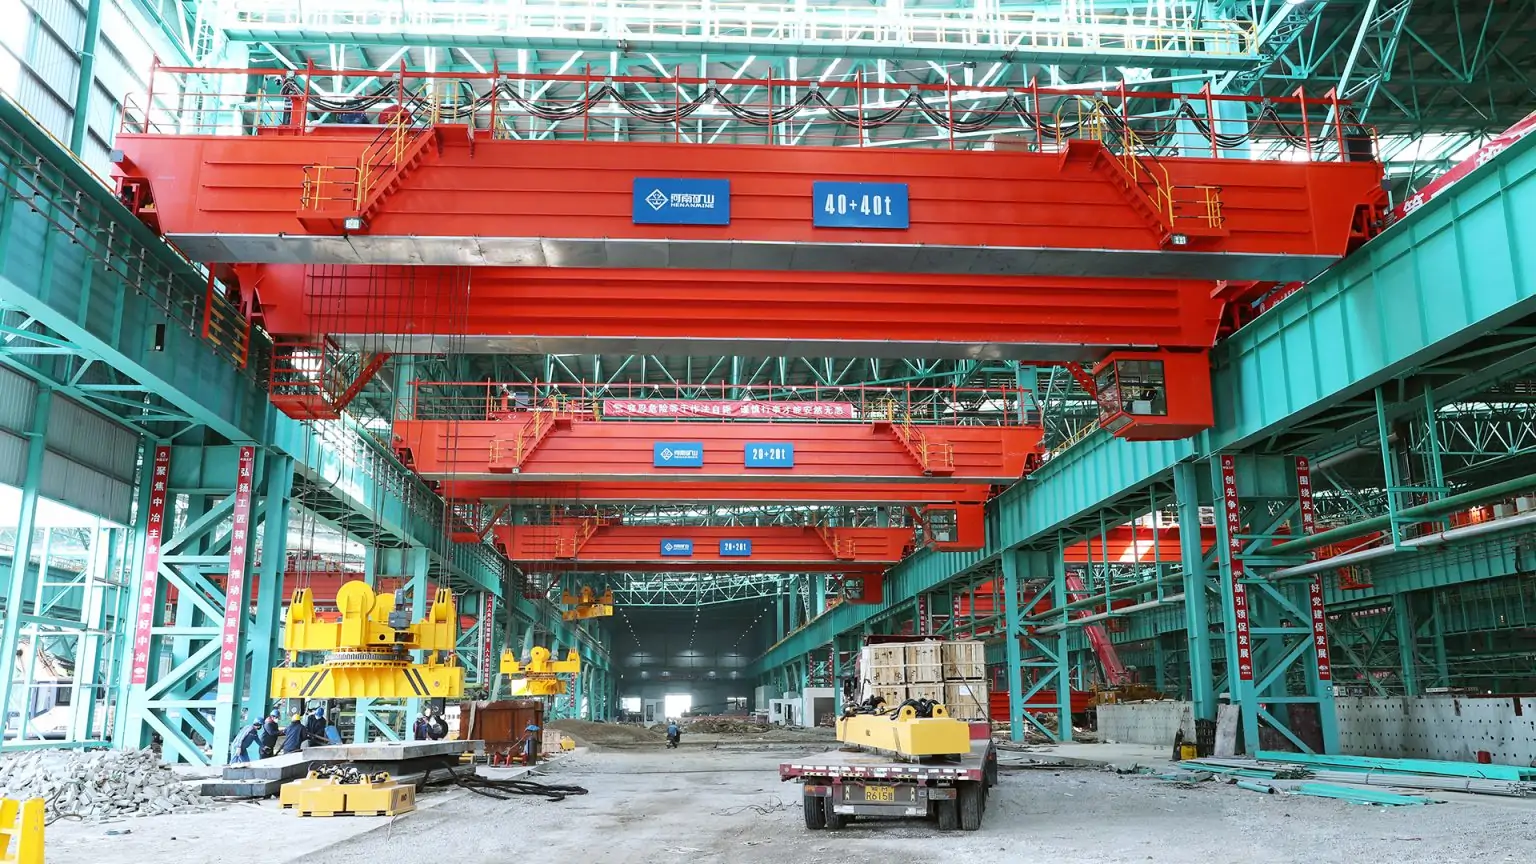
    heat-protected heavy-duty bridge crane in a high-temperature steel processing environment
    Thermal protection is based on actual exposure at each component. Workpiece temperature alone does not define the temperature experienced by the crane.

    Manual, Semi-Automatic and Integrated Forging Operation

    The control level follows process repeatability, visibility, cycle time, exception rate and the production system’s ability to provide dependable interlocks and workpiece data.

    Control Level Typical Functions Suitable Operating Pattern Definition Required
    Manual control Cabin or radio control, variable speeds, load display, cameras and interlocks Mixed workpieces, frequent exceptions and operator-led rigging Sightlines, control location, communications, exclusion zones and permitted motions
    Semi-automatic Stored positions, automatic travel profiles or assisted turning with operator authorization Repeated stations with controlled workpiece families Coordinates, confirmation logic, permissible sequence and exception recovery
    Press-line integrated Signal exchange with press, manipulator, furnace and safety control systems High-repeatability open-die forging and coordinated production Signal list, ownership, timing, safe states, independent stops and commissioning protocol
    Automatic material flow Task receipt, route control, positioning, status feedback and production-data exchange Controlled transfer between fixed stations with limited human access Plant interface, zone control, workpiece identity, cybersecurity and manual fallback
    Henan Mine Crane automated metallurgical crane platform relevant to integrated forging material flow
    Integrated operation requires an agreed signal matrix, safe-state philosophy, independent emergency functions and a tested manual-recovery procedure.

    Design Basis, Inspection and Acceptance

    The purchase specification identifies one coherent design route. Local statutory requirements at the installation site remain applicable, and standards from different systems are not selectively combined without an approved compliance matrix.

    Possible Design Routes

    A project may use ISO 4301 classification principles with applicable crane standards; EN 13001 with EN 15011 and EN 13155 where applicable; or a North American route using CMAA 70 with applicable ASME B30.2, B30.20 and ASME BTH-1 requirements. The contract states the selected basis and local additions.

    Engineering Deliverables

    General arrangement, load-case schedule, duty calculation, wheel loads, clearance and turning study, attachment data, thermal assessment, electrical drawings, control narrative, interface list, inspection plan and maintenance-access arrangement.

    Manufacturing Inspection

    Material traceability, welding procedures and welder qualification, specified NDT, dimensional checks, machinery alignment, drum and rope inspection, attachment inspection, electrical-panel tests, coating and document review.

    FAT and Site Acceptance

    Functional tests verify motions, brakes, limits, overload protection, control modes, alarms and interfaces. Site testing then covers runway, erection, proof load, representative workpieces, turning sequence, power-loss response, positioning, press coordination, training and handover.

    Acceptance Item Verification Recorded Evidence
    Rated and governing load cases Contractual proof/load test and functional motion checks Test procedure, calibrated instruments and signed results
    Turning and attachment Approved representative workpieces across the declared envelope Workpiece list, sequence, grip/rigging checks and exception record
    Safety and controls Limits, overload, stops, interlocks, communication loss and fallback modes Cause-and-effect record and completed test sheets
    Handover readiness Training, spares, manuals, inspection plan and maintenance access Handover dossier, punch-list closure and acceptance certificate

    Relevant Heavy Metallurgical Crane Experience

    Relevant references are evaluated by capacity, thermal exposure, duty, trolley architecture, process control and commissioning complexity. The following published Henan Mine Crane projects demonstrate adjacent engineering capability; a new forging crane still requires its own process and load-case validation.
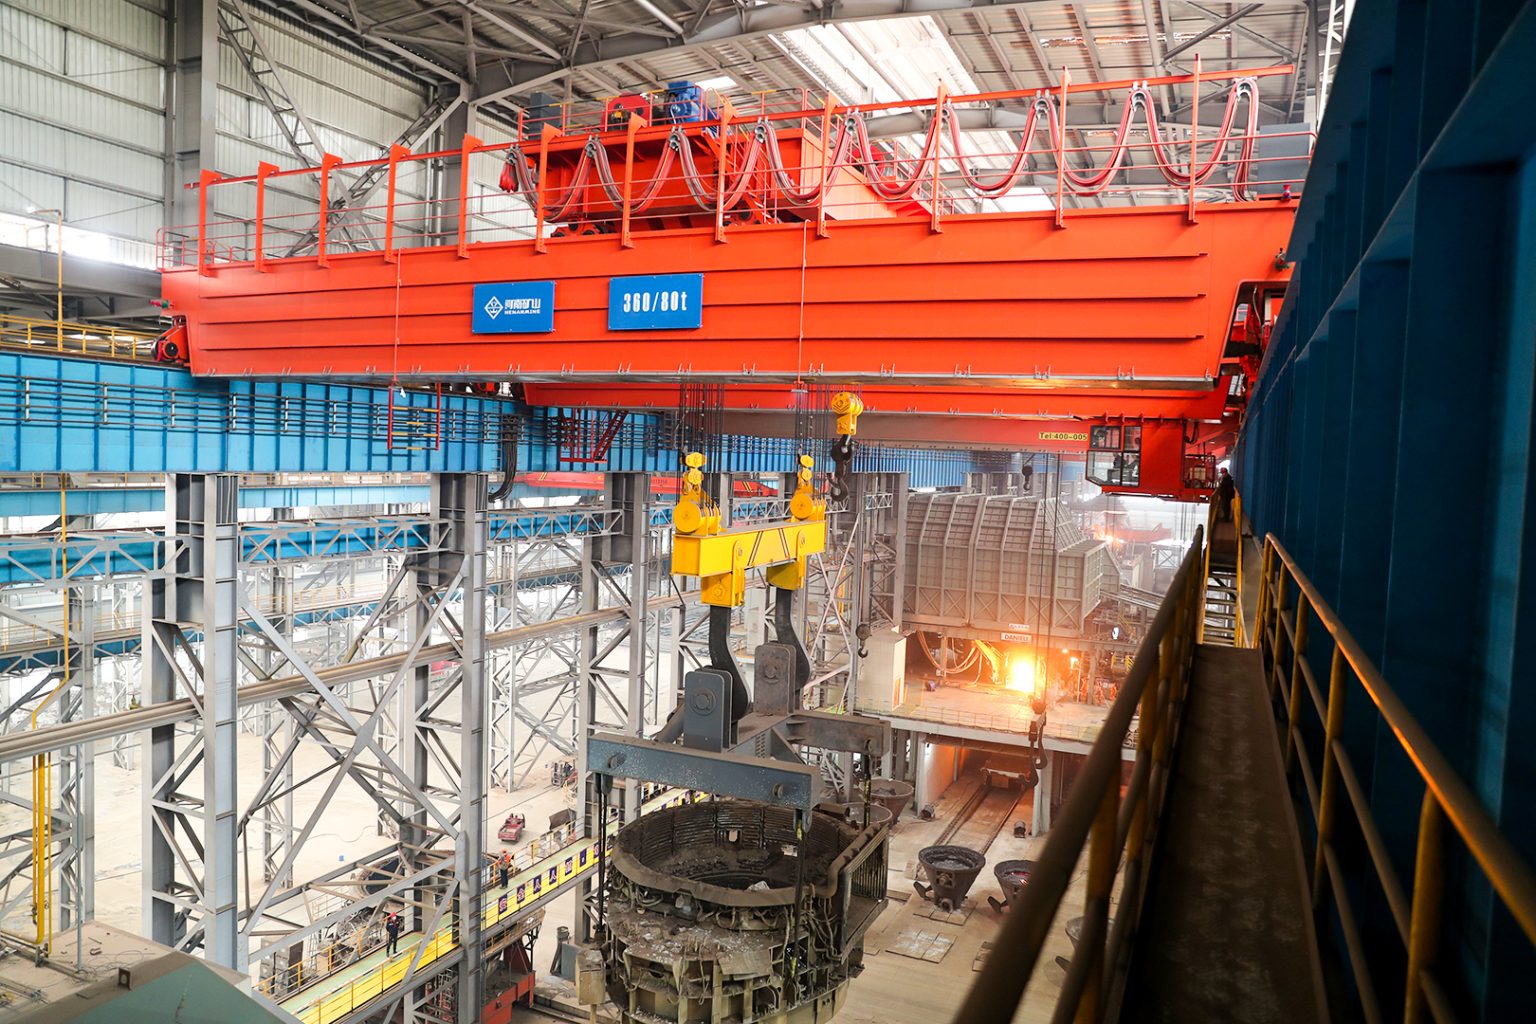
    Henan Mine Crane 360 ton four-girder foundry crane heavy metallurgical project

    Ultra-Heavy Metallurgical Reference

    360 t Four-Girder Foundry Crane

    The published Jinsheng’an Group project uses a four-girder, four-rail, dual-trolley arrangement for a 360 t foundry duty, with heavy-capacity structure, thermal protection and redundant hoisting functions.

    The reference is relevant to ultra-heavy structure, trolley coordination and high-temperature engineering. Its molten-metal duty does not define the attachment, motion sequence or safety architecture of a forging crane.
    View 360 t Project Reference

    Henan Mine Crane hot-rolled steel plant specialized bridge crane project

    High-Temperature Production Reference

    Hot-Rolled Steel Plant Bridge Cranes

    Henan Mine Crane publishes a 50–200 t, A6 specialized bridge-crane platform for hot-rolling production, with project-defined heat protection, variable-frequency control and production-system integration.

    This experience is relevant to radiant-heat exposure, continuous steel-plant operation and equipment interfaces. Forging impact, turning and attachment requirements remain separate design inputs.

    View Steel-Plant Reference

    Reference boundary: adjacent metallurgical projects demonstrate relevant structural, mechanism, thermal-protection and control experience. They do not establish the final capacity, duty, turning device, cycle performance, compliance or price of a new forging crane.

    Forging Crane Price and Budget Scope

    A reliable forging crane price requires the maximum gross suspended load, turning method, span, lift, duty, speeds, thermal exposure, controls, runway scope, destination and acceptance requirements. Public listings provide only preliminary market signals because they rarely normalize the process attachment, safety functions or project boundary.

    Public Market Signal Checked in September 2026 Published Position Budget Meaning Commercial Limitation
    25 t double-girder crane marketed for forging; 14 m span and 10 m lift US$42,000 per set A public equipment-level signal for a smaller forging application Attachment, heat duty, runway, freight, erection, tests and local compliance are not normalized
    General double-girder listing with maximum lifting weight above 200 t US$5,000–500,000 per set Shows how capacity-only marketplace ranges become too broad for project budgeting Not a forging-specific quotation and may include placeholder endpoints
    Dedicated heavy forging cranes publicly presented at 180–550 t Price on request Heavy press-shop systems are treated as engineered capital projects Capacity does not reveal trolley layout, turner, duty, thermal design or installation scope
    Henan Mine Crane forging system Project quotation Technical and commercial scope is built from the approved forging process and site data A comparable price requires the RFQ inputs listed below

    Major budget drivers: gross suspended load; main/auxiliary or dual-trolley arrangement; tongs, turner or other below-hook device; span, lift and hook approaches; duty and process dynamics; heat shielding and cooling; braking and redundancy; cabin, cameras and controls; press/MES integration; runway and electrification; export packing, freight, erection, testing, training and local certification.

    The figures above are third-party public market observations, not Henan Mine Crane offers. Marketplace values may be equipment-only figures, placeholders or scopes that exclude essential engineering and site work. Contract comparisons require a line-by-line technical and commercial reconciliation.

    Forging Crane RFQ Information

    A complete enquiry allows the structure, hoists, turning system, thermal protection, runway reactions, controls and commercial scope to be priced on the same basis.

    Workpiece and Attachment Data

    Minimum, typical and maximum mass and dimensions; temperature at pickup; center of gravity; material and surface; dies and tooling; required tongs, clamp, turner, spreader or rigging; drawings and photographs.

    Process and Duty

    Furnace, press, hammer, manipulator and heat-treatment sequence; lifts and turns per hour; shifts; annual hours; load spectrum; required cycle time; permitted process forces and production consequence of downtime.

    Workshop and Runway

    Rail-center span, runway length, rail and elevation; required lift; headroom and approaches; existing wheel-load limits; press, furnace, platform and duct drawings; installation access and site-survey data.

    Controls and Commercial Scope

    Cabin, radio or automatic control; positioning tolerance; press/MES protocol; voltage and frequency; environment; destination; compliance route; Incoterm; runway, electrification, installation, commissioning, testing and documentation scope.

    Fastest route to a comparable proposal: provide a workshop cross-section, equipment layout, workpiece matrix, step-by-step handling sequence and required supply boundary. When existing information is incomplete, the quotation can separate confirmed scope, provisional allowances and exclusions.

    Frequently Asked Questions

    How is forging crane capacity calculated?

    Capacity begins with the maximum workpiece and adds tongs, turning device, spreader, rigging, hook blocks and other suspended equipment. The design then evaluates off-center loads, main/auxiliary load sharing, dynamics and the selected duty classification.

    Is a forging crane the same as a foundry crane?

    No. A forging crane principally handles solid ingots, dies and forgings and may assist rotation at a press. A foundry crane handles ladles and molten metal under a different risk profile and safety architecture.

    When are main and auxiliary hooks required?

    They are considered when the approved process requires tailing, turning, secondary positioning or tool handling. Hook spacing, capacity split, simultaneous loading and the complete rotation sequence must be defined before selection.

    Can a standard overhead crane handle hot forgings?

    Only after a dedicated engineering review. Radiant heat, scale, duty, process dynamics, attachment, visibility and component temperatures can require structural, mechanical, electrical and control measures beyond a general-purpose crane.

    How much does a forging crane cost?

    A public 25 t forging-application listing reviewed in September 2026 showed US$42,000 per set, while dedicated 180–550 t forging cranes were generally price-on-request. Final cost depends on the full process, attachment, thermal design, duty, runway, controls and delivery scope.

    Can a forging crane coordinate with a hydraulic press?

    Yes, when the crane, press, manipulator and safety systems share an approved functional specification. The signal matrix defines command ownership, permissives, timing, safe states, independent stops and recovery after a fault.

    Can an existing runway be reused?

    Only after the rails, beams, brackets, columns, connections and foundations are checked for condition, alignment, fatigue and the new crane reactions. Heavy process trolleys and special attachments can change wheel loads materially.

    What should be tested before handover?

    Testing covers motions, brakes, limits, overload protection, control modes, attachment functions, representative workpieces, turning sequences, power-loss response, positioning, interfaces, safety zones and manual recovery under agreed criteria.

    Request a Forging Crane Quote

    Submit the workpiece and attachment matrix, temperature, forging sequence, lifts and turns per hour, press, furnace and manipulator drawings, span, lift, runway data, required control level, power supply, destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.
    Henan Mine CraneDiscuss your requirements ↗
  • Overhead Bridge Crane

    Overhead Bridge Crane

    Overhead Bridge Crane

    Henan Mine Crane · Workshop and Industrial Lifting

    Overhead Bridge Crane

    An overhead bridge crane moves a suspended load vertically and across a working bay. A hoist or trolley travels along the bridge, while the bridge runs on elevated runways to serve production stations, storage areas and loading positions.

    Henan Mine Crane manufactures single-girder, double-girder and underhung overhead bridge cranes for industrial material handling. Configure the crane around the load, required hook coverage, building structure and operating duty, with the equipment and installation interfaces defined in your quotation.

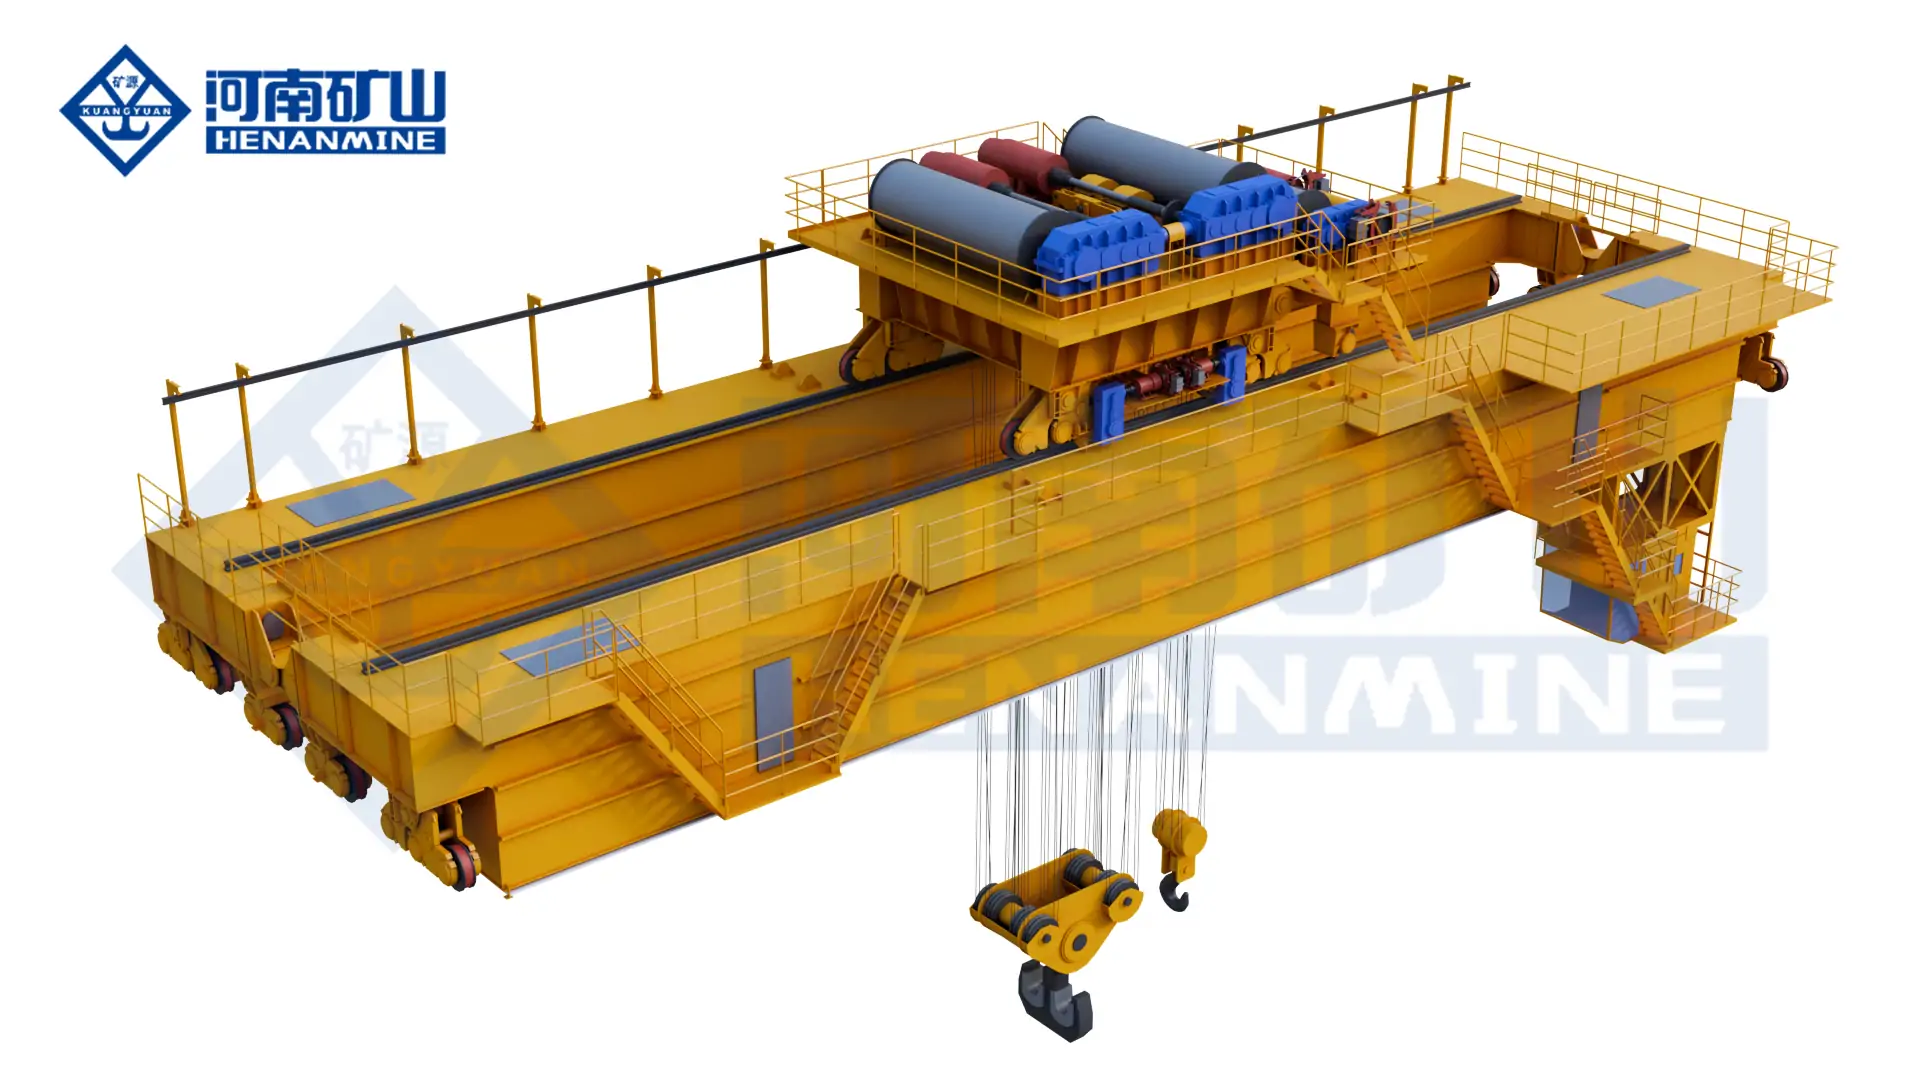
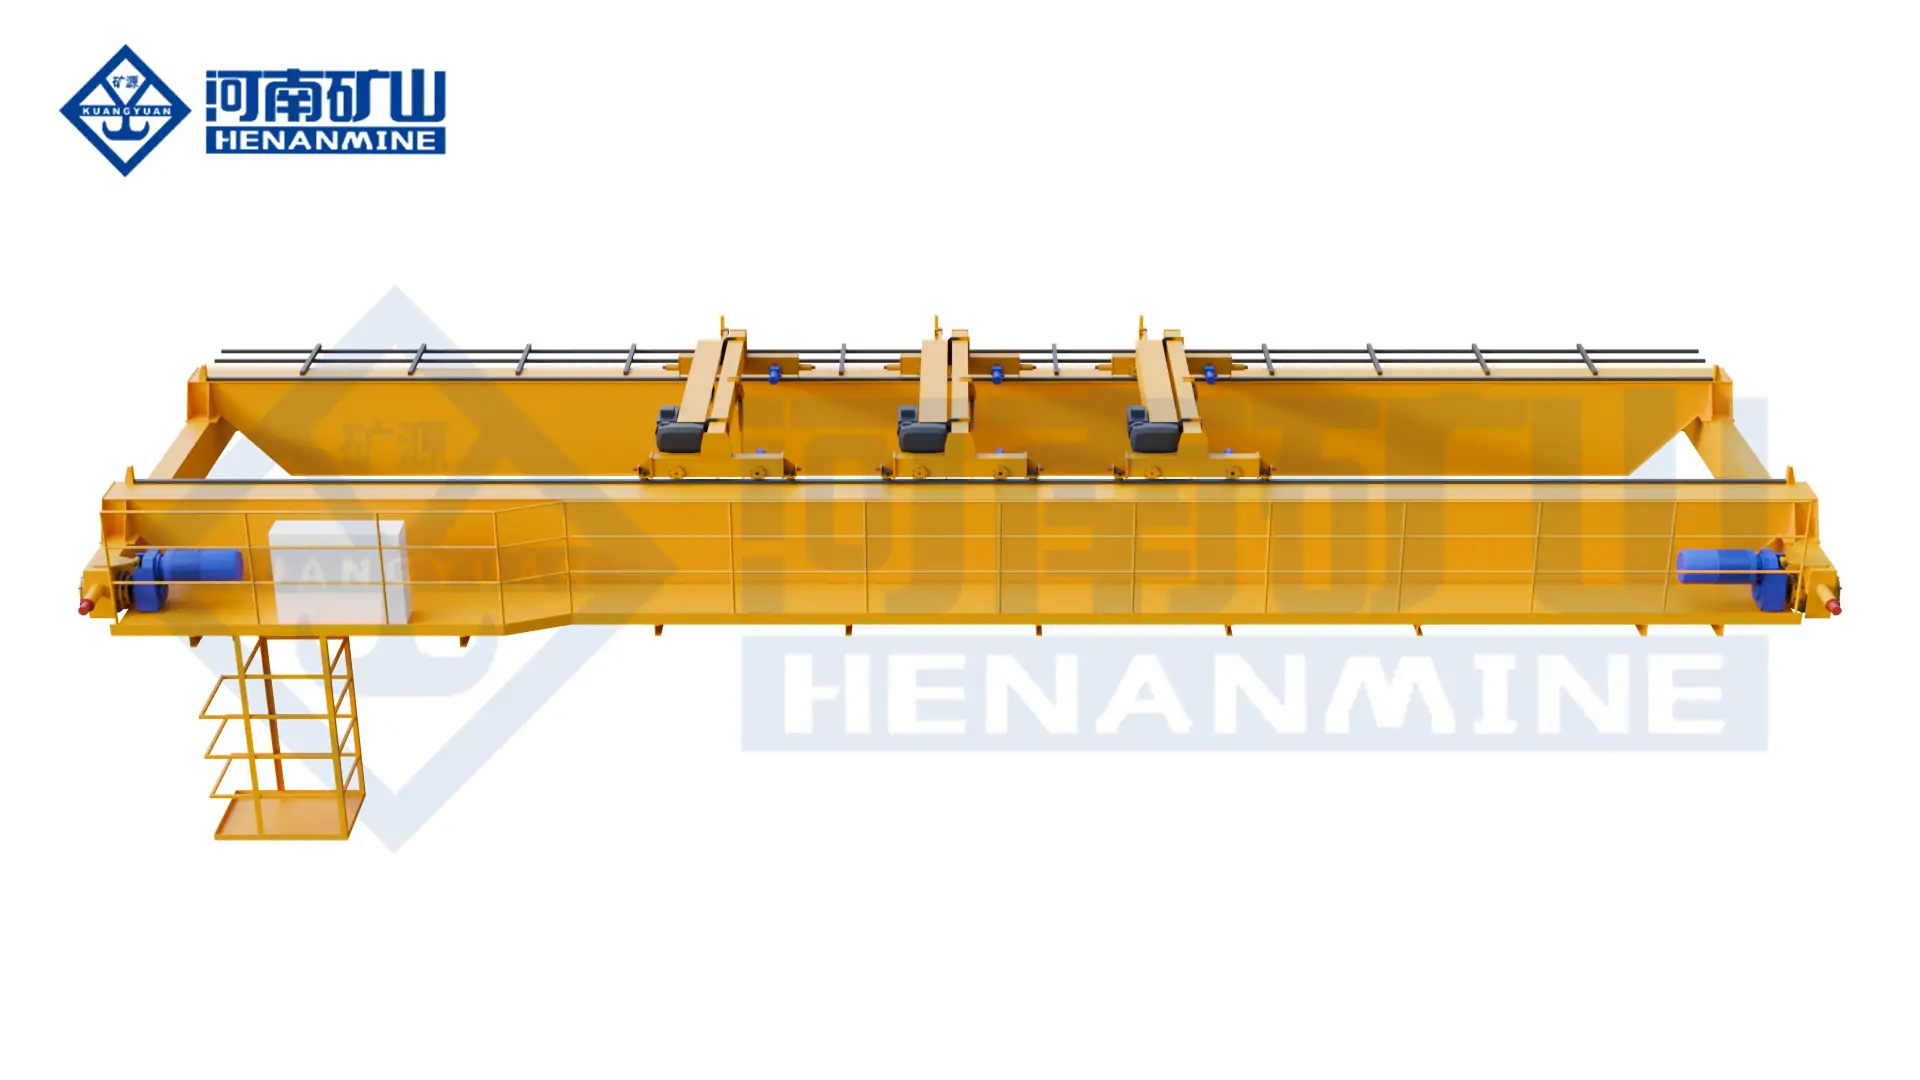
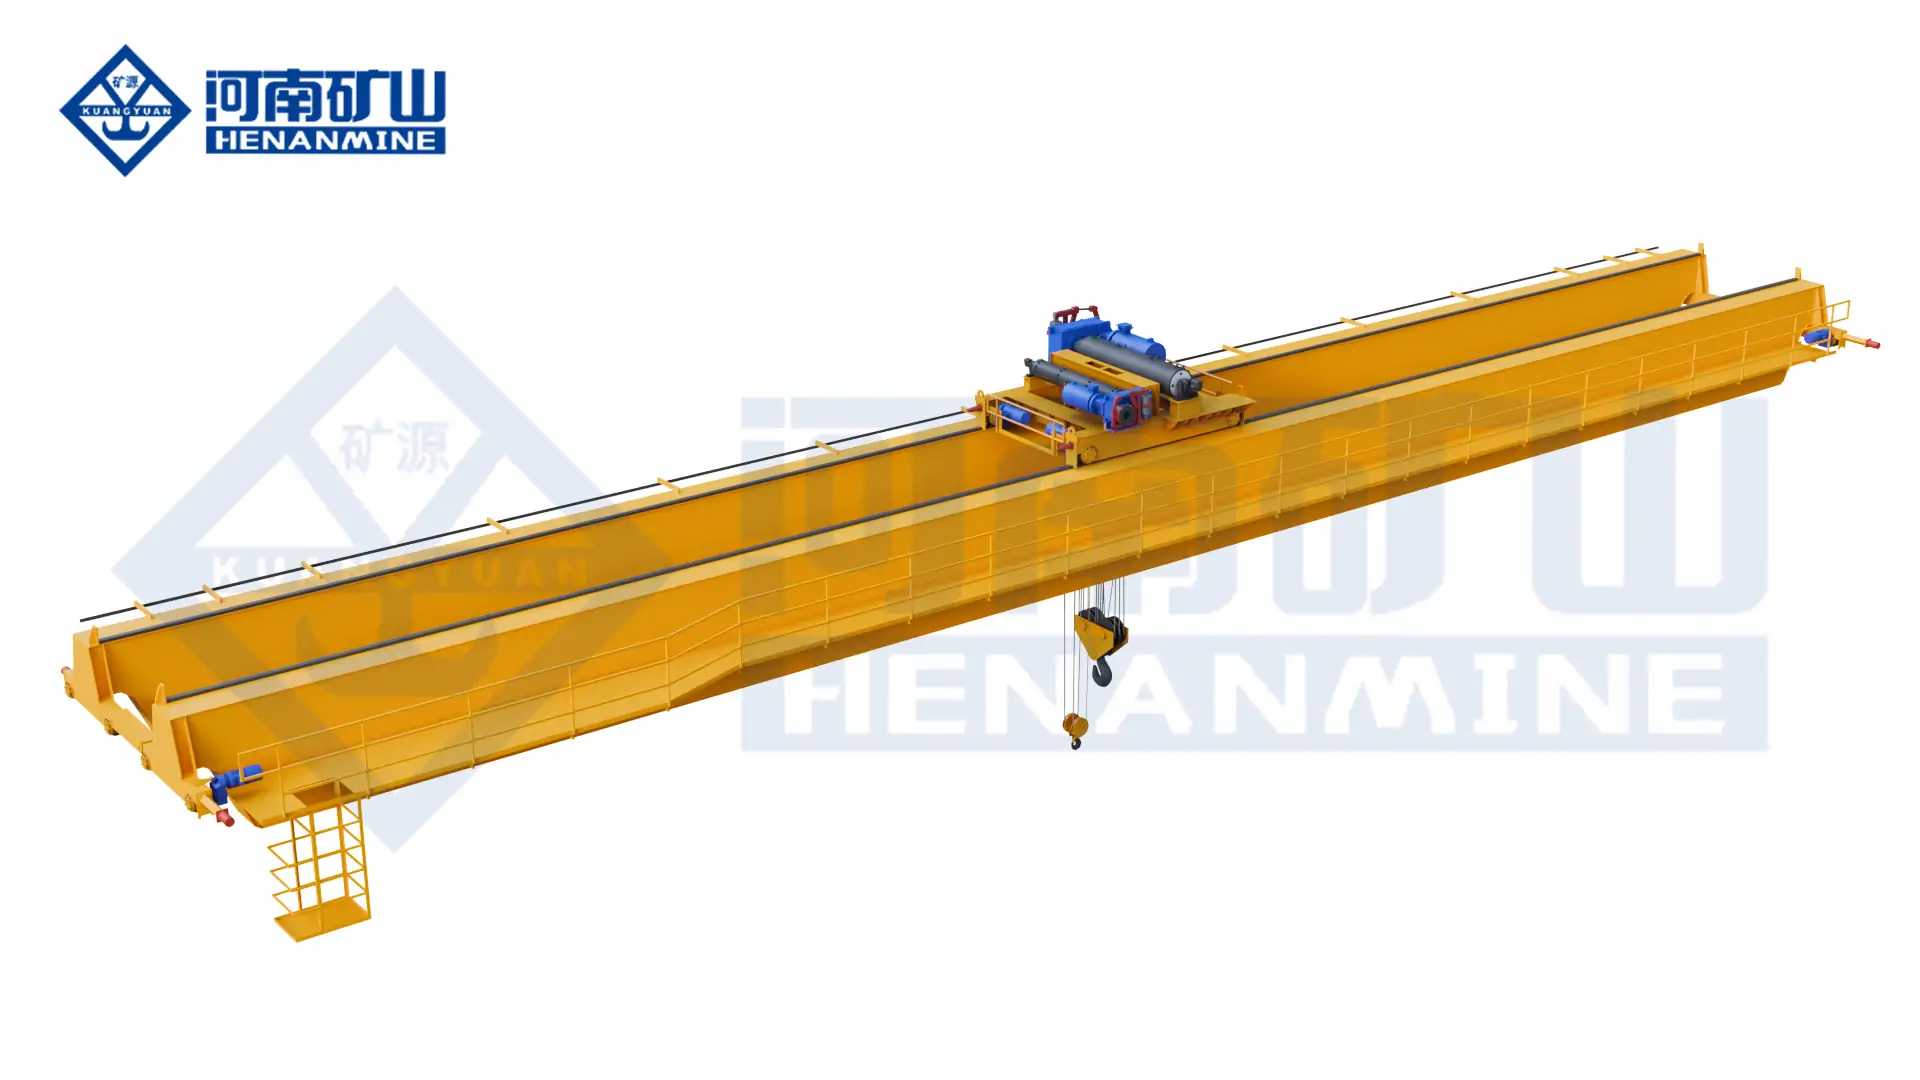
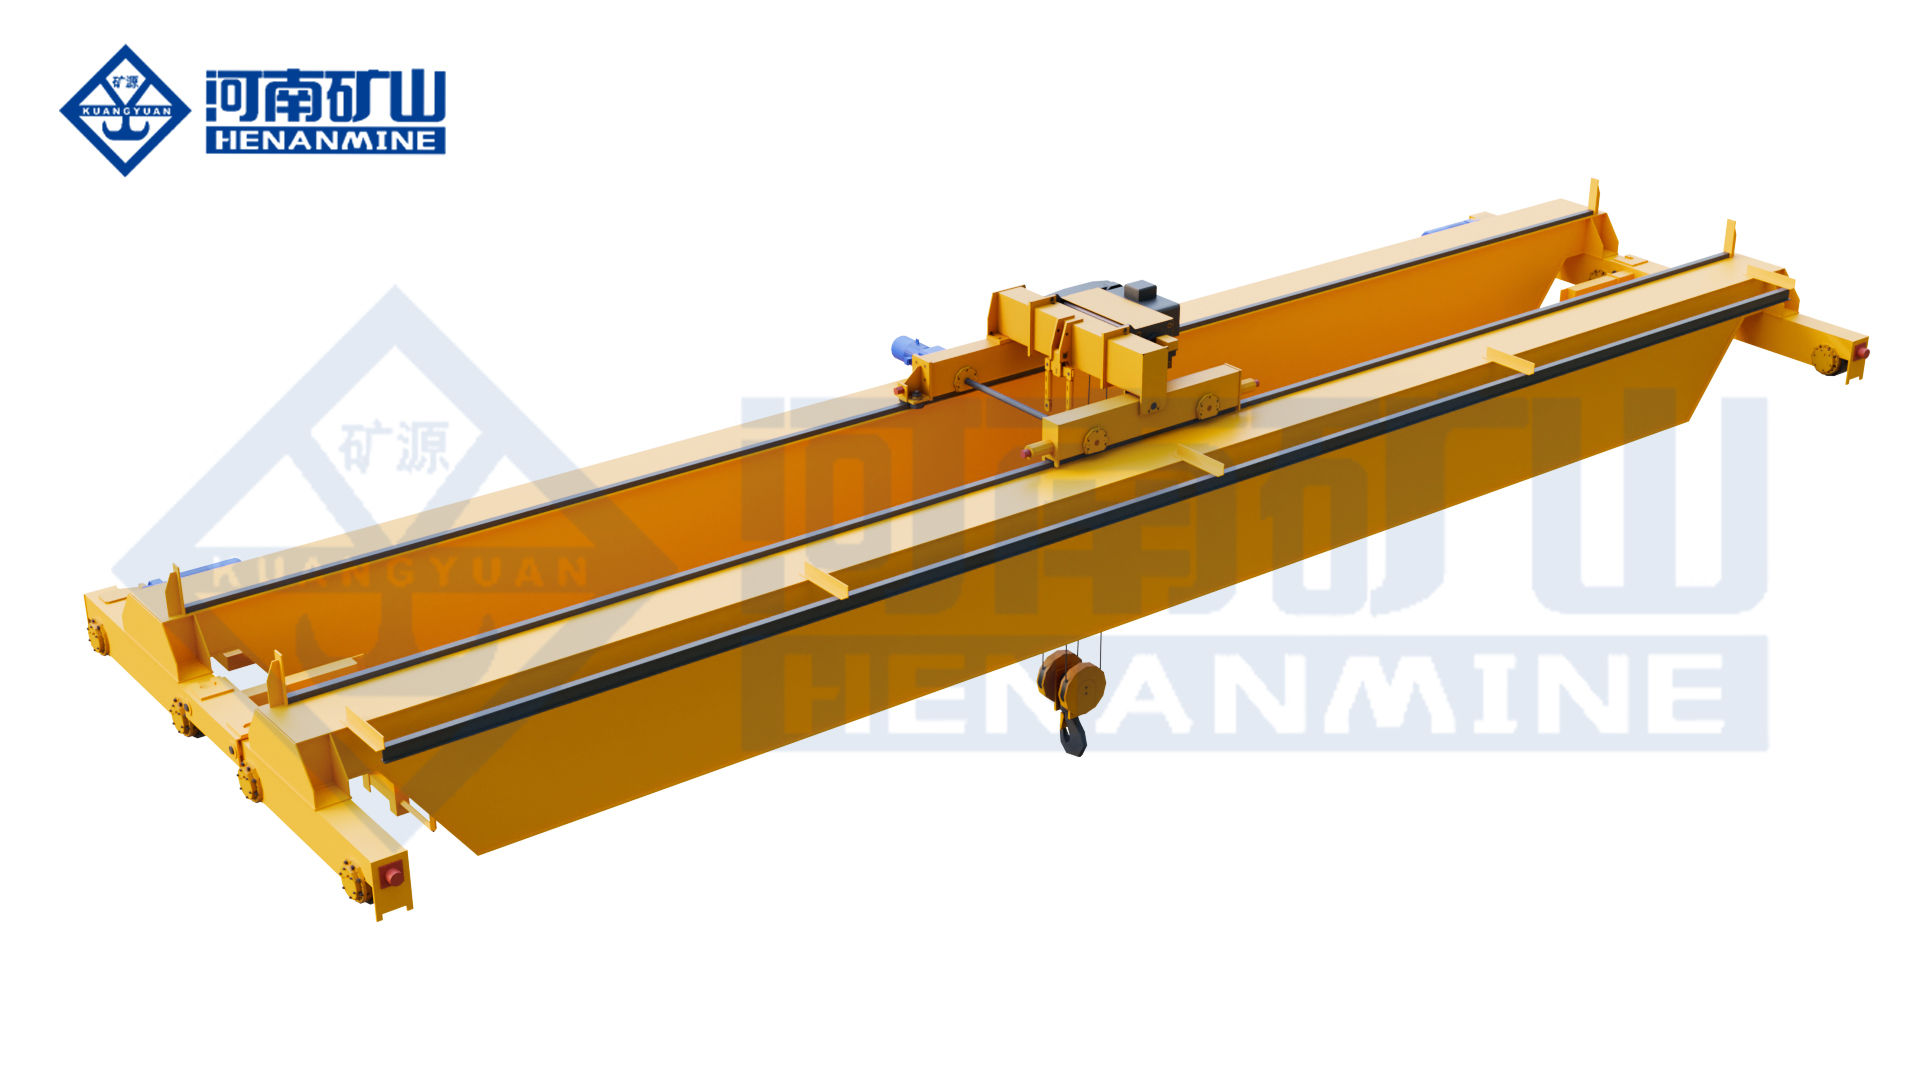
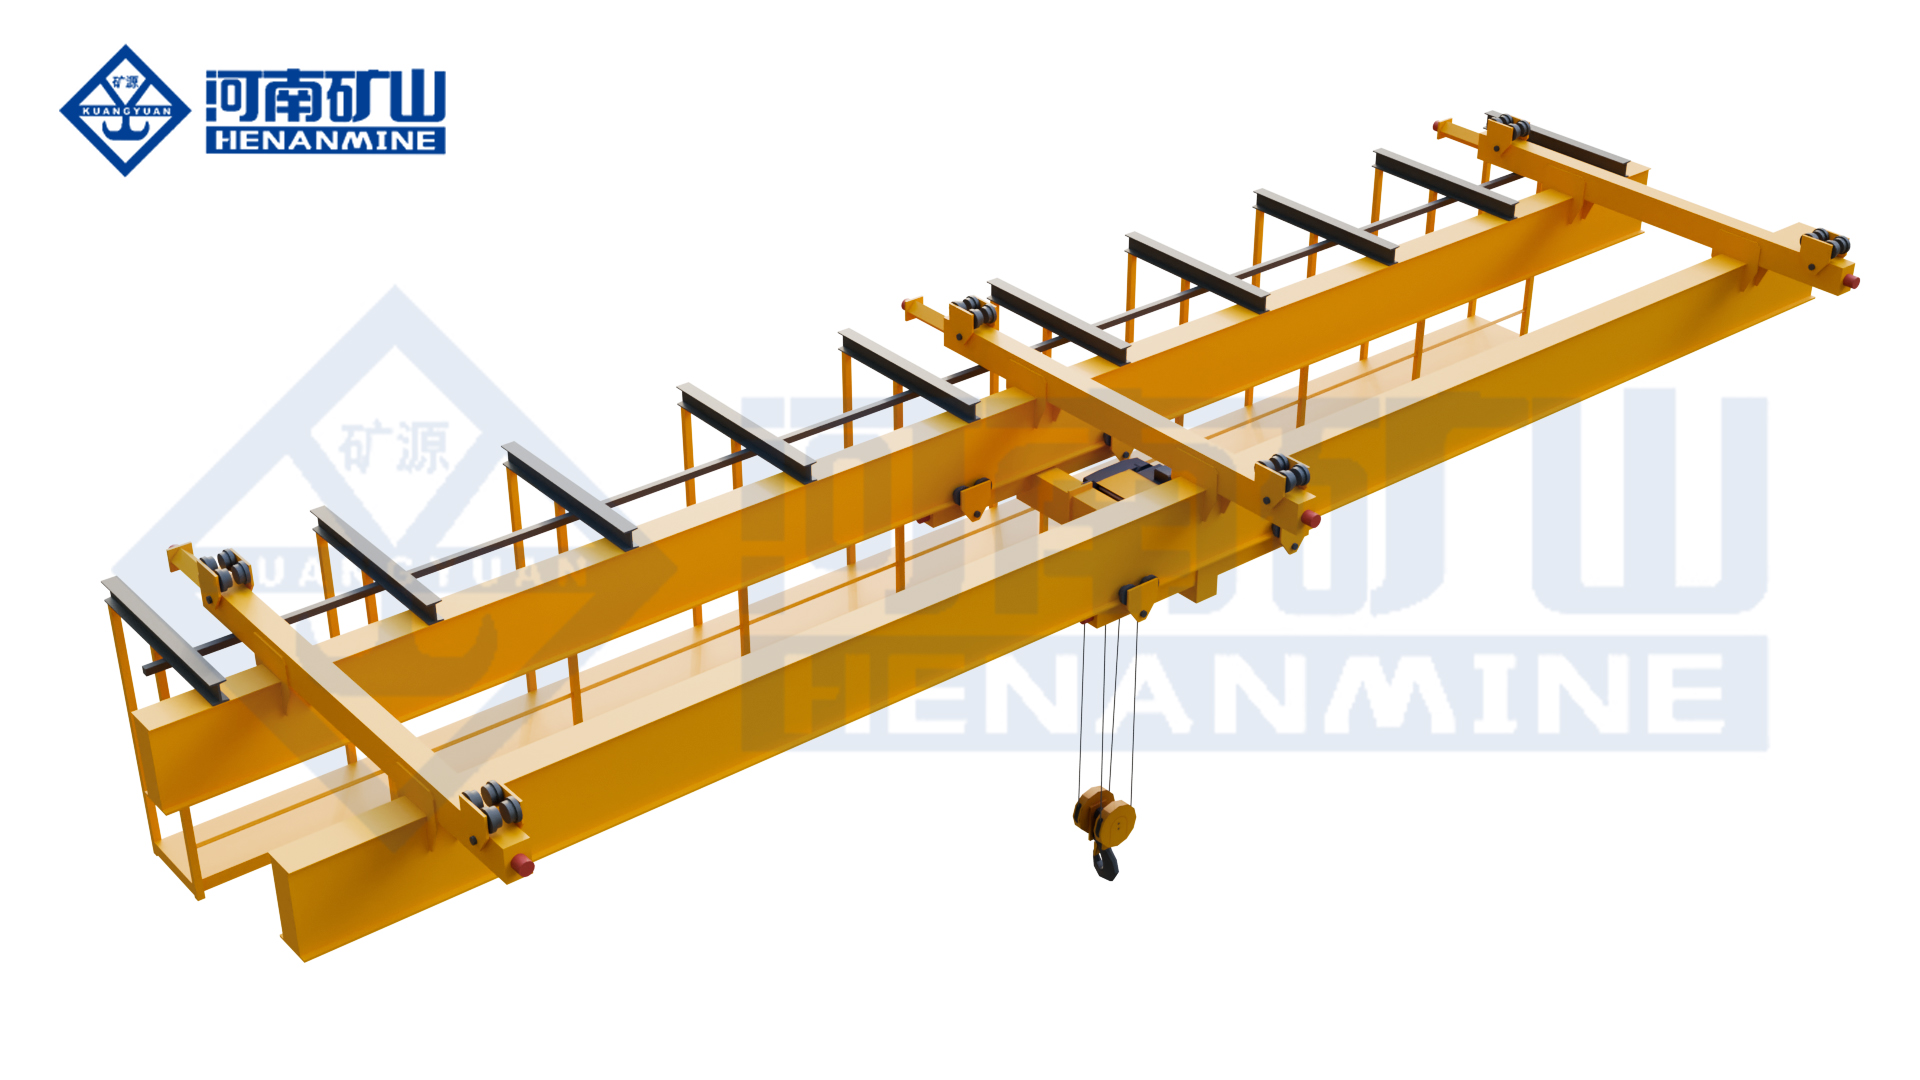
    Double-girder overhead bridge crane with an electric-hoist trolley from Henan Mine Crane
    Double-girder overhead bridge crane with an electric-hoist trolley. The installation drawing defines the span, hook levels and runway interfaces.

    BRIDGE DESIGN

    Single or Double Girder

    RUNWAY ARRANGEMENT

    Top Running or Underhung

    LIFTING EQUIPMENT

    Hoist or Trolley to Suit the Task

    PROJECT INTERFACES

    Load, Coverage, Structure and Power

    Overhead Bridge Cranes for Workshops and Warehouses

    Overhead crane and bridge crane are common names for this arrangement. Electrically powered travelling models are also called EOT cranes. The practical selection starts with the material flow and the space the hook must reach.

    Connect Production Stations

    Transfer components between fabrication, machining and assembly positions within one crane bay. Include the load orientation and lifting attachment required at each station.

    Serve Storage and Loading Areas

    Reach designated storage lanes and loading positions from above. Check obstructions, vehicle access and the available hook approach at the ends of the runway.

    Handle Maintenance Lifts

    Lift equipment clear of its mounting and move it to a service area. Allow enough hook height for the lifting gear and enough horizontal clearance for the complete component.

    The load path remains within the crane’s defined coverage. Supporting columns, runway steelwork, overhead services and maintenance access still need to be accommodated in the facility layout.

    Overhead Bridge Crane Technical Specifications

    The references below correspond to the linked Henan Mine Crane product tables. They help shortlist an arrangement; the final project specification also defines duty, speed, hook approaches and structural reactions.

    Product Reference Rated Capacity Span Lifting Height
    Single-Girder Bridge Crane: Selected Examples 5 t and 10 t 7.5–28.5 m, listed spans 6, 9, 12, 18, 24 or 30 m
    LH Double-Girder Electric-Hoist Bridge Crane 3–32 t 7.5–31.5 m 6–30 m
    Single-Girder Suspended Bridge Crane 1–10 t 7.5–28.5 m 6–20 m

    All t values here are metric tonnes. If your project uses US short tons, identify that unit in the enquiry. Confirm the complete load, span and lifting-height combination for the selected model; maximum catalogue values are not automatically available together.

    Additional Technical Inputs

    • Maximum and typical cargo weights, load dimensions, centre of gravity and lifting gear.
    • Runway length and elevation, highest and lowest required hook positions, and coverage at each workstation.
    • Lifts per hour, load distribution, operating shifts, travel distances and positioning needs.
    • Supply voltage, frequency and phases; control method; environment and required design standard.
    • Wheel loads, wheel spacing, runway interfaces, access platforms and agreed installation scope.

    Selection Considerations

    01 / LOAD

    Start with the Lifted Load

    Describe the cargo and the slings, lifting beams, grabs or other attachments. Their weights and geometry affect the required rating, hook height and usable payload.

    02 / COVERAGE

    Map the Working Area

    Mark every pickup and placement point on the building plan. Include machine enclosures, doors, stored goods and services that could restrict the load or hook path.

    03 / OPERATION

    Match the Production Duty

    Separate occasional maintenance lifting from repetitive production handling. Load spectrum, operating time and travel distances help determine the crane and mechanism duties.

    04 / INSTALLED SCOPE

    Review the Complete Installation

    Compare the crane with its runway, supporting structure, power supply and service access. A lower equipment price can come with a different building or installation requirement.

    Overhead Bridge Crane Compared with Other Industrial Crane Configurations

    Girder count and runway arrangement are separate choices. A single-girder crane can have a top-running bridge with an under-running hoist; the position of that hoist does not classify the bridge as underhung.

    Configuration Structural Arrangement Selection Trade-Off
    Single-Girder Overhead Bridge Crane One main girder, commonly with a travelling hoist below the beam. A compact arrangement for general handling. Compare hook height, side approaches, duty and total installed cost.
    Double-Girder Overhead Bridge Crane Two main girders carrying the selected trolley and lifting mechanism. Allows different trolley and hook arrangements. Review crane height, runway loading and maintenance access for the proposed layout.
    Underhung Overhead Bridge Crane The bridge travels on the lower flanges of suitable elevated runway beams. Useful where the building supports a suspended runway layout. Flange loading, connections and supporting steelwork require assessment.
    Multi-Support Underhung Bridge Crane A suspended bridge uses multiple runway supports across the working area. Consider for an engineered multi-rail facility. Coordinate support locations, alignment and the distribution of loads.
    Gantry Crane Legs carry the bridge above ground-level runways or a specified travel system. An alternative where elevated runways are unsuitable. Account for leg clearance, travel lanes, ground conditions and foundations.

    For a top-running overhead bridge crane, the end carriages run on rails above the runway beams. Those runways may be carried by building columns or by an independent engineered support structure.

    Hook Coverage, Headroom and Load Clearance

    Span Is Not Hook Coverage

    Span is based on the runway centreline spacing. Side and end approaches, together with any engineered overhang, determine where the hook can travel. Check the resulting working area against the layout.

    Lifting Height Is Not Building Height

    Determine the required highest hook position from the load, lifting gear and obstacle clearance. Then check the complete crane envelope against roof members, lighting, ductwork and maintenance space.

    The Load Needs Clearance Too

    A reachable hook position does not guarantee that a long beam or bulky machine can pass through the same area. Check the suspended load’s dimensions and intended orientation along the full route.

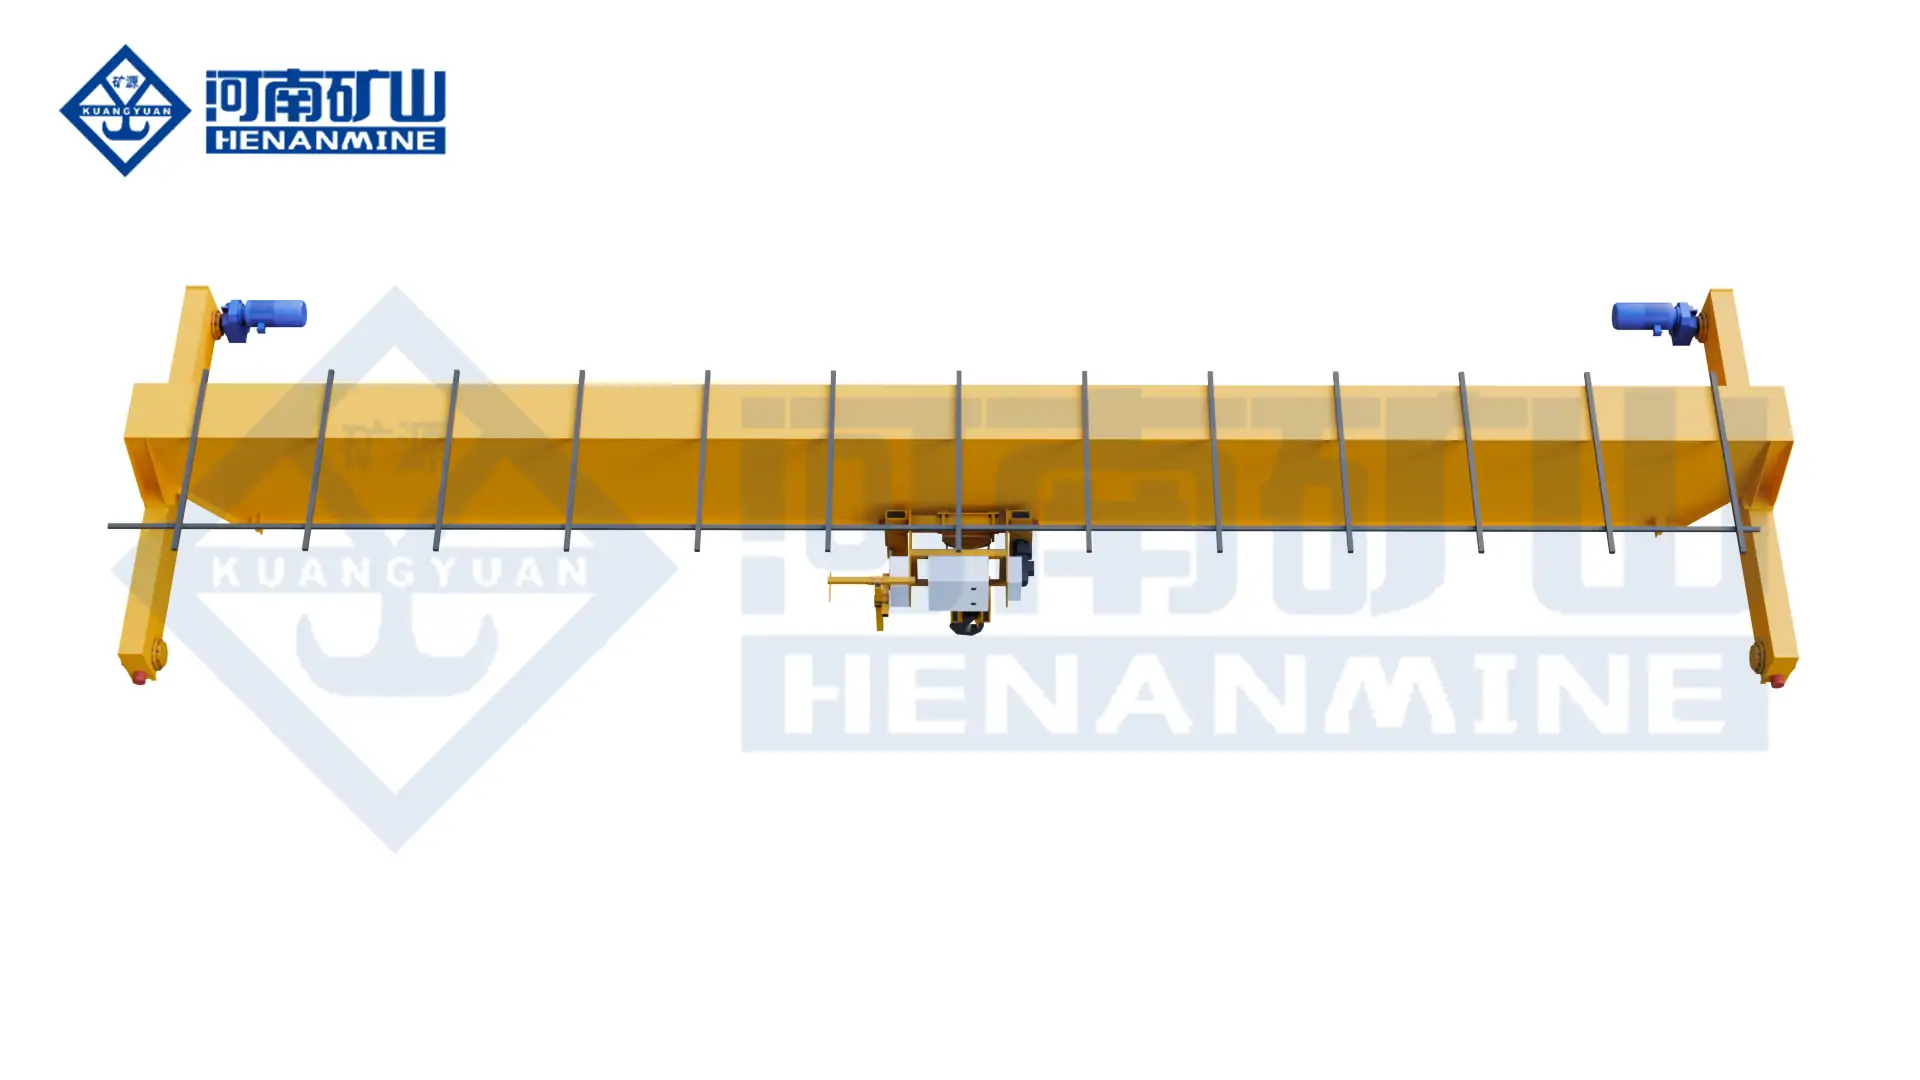
    Single-girder overhead bridge crane with a travelling hoist below the main girder
    Single-girder bridge with an under-running hoist. The hoist position and end clearances influence the working envelope.
    Multi-support double-girder underhung overhead bridge crane with several runway beams
    Multi-support underhung arrangement. Runway support positions and load distribution are coordinated with the building structure.

    For restricted headroom, compare a low-headroom hoist and alternative bridge layouts on the same building cross-section. The useful result is the achievable hook level with the required clearances and access.

    Runway Loads and Building Support

    Runway selection is part of the crane installation. Crane deadweight, trolley position, lifted load and the agreed design load combinations influence the forces transferred to the building or independent supports.

    New Building

    Coordinate the crane drawing with the structural design before fixing runway elevations and column positions. Include power routes, end clearances and access to the lifting and travel equipment.

    Existing Building

    Survey the rails, runway beams, connections and supporting structure. Use the proposed wheel loads, wheel spacing and horizontal reactions for the structural review.

    Replacement Crane

    Compare the actual interfaces of the old and proposed cranes. The same rated capacity can come with different crane weight, wheelbase, loading, hook approaches and electrical demand.

    Define who supplies the runway beams, rails, columns, brackets and foundations. The crane quotation and the building design should use the same approved installation data.

    Hoists, Trolleys and Operating Duty

    Choose the lifting mechanism around the load and work cycle. A double-girder structure does not by itself establish heavy-duty or continuous-service capability; both the crane and its individual mechanisms need suitable classifications.

    Hoist or Trolley Arrangement

    Compare the selected hoist layout, lifting height, hook block, maintenance access and available speeds. The arrangement also affects the hook approaches and structural loads.

    Main, Auxiliary or Dual Hoists

    Identify the task for each hook and any permitted combined operation. Ratings, hook separation, shared loads and control coordination must be defined for multi-hook handling.

    Operating Cycle

    Record the frequency of near-rated lifts, mechanism running time, starts and travel distances. These inputs help distinguish intermittent workshop use from repetitive production service.

    For long components, review the double-trolley electric-hoist bridge crane arrangement. For controlled speed and acceleration, compare the frequency-conversion electric-hoist overhead crane. Specify the required performance for each motion.

    Controls, Power Supply and Motion Performance

    Pendant, Radio or Cabin Control

    Select around operator visibility, walking routes and the handling task. Multiple control stations require a defined selection priority and response to a loss of command signal.

    Power Feed and Distribution

    Confirm site voltage, frequency, phases and the connection point. Distinguish the runway power system from the cable or conductor arrangement supplying the moving hoist or trolley.

    Speed and Positioning

    Specify hoisting, trolley travel and bridge travel separately. Include acceleration, stopping and placement needs; maximum travel speed alone does not define the handling cycle.

    Anti-sway, automatic positioning, load monitoring and production interfaces are functions to specify individually. Agree their operating conditions and acceptance method before they become part of the supply scope.

    Attachments, Special Environments and Safety

    A general workshop hook crane is only one configuration. The material and environment can change the lifting attachment, mechanical design, controls and protection requirements:

    • Grab overhead cranes handle suitable bulk materials. Supply material density, condition, required throughput and discharge height so grab payload and crane duty can be selected together.
    • Explosion-proof overhead cranes require the site’s hazardous-area classification and relevant gas or dust information. Equipment protection and documentation must match that application.
    • Metallurgical bridge cranes address defined hot-material and production duties. Describe the process, temperature exposure and consequences of a lifting interruption.
    • Outdoor or corrosive locations require review of weather exposure, coatings, electrical protection, runway conditions and relevant wind requirements.

    Protection and Safety Functions

    Define overload protection, hoisting and travel limits, braking, emergency stops and electrical protections for the selected crane. Shared runways need an assessment of crane separation and collision prevention. Additional brakes, monitoring or redundancy arrangements depend on the intended duty and risk assessment.

    Manufacturing and Inspection Documentation

    Henan Mine Crane manufacturing workshop showing crane bridge structures and lifting mechanisms
    Crane structures and lifting equipment inside a Henan Mine Crane production workshop.

    Henan Mine Crane manufactures overhead lifting equipment for industrial production and material handling. View the company’s manufacturing workshops for published factory photographs.

    The order documentation should connect the selected crane configuration with the equipment supplied. Agree the following requirements before manufacture:

    • General arrangement drawing showing rated capacity, span, hook limits, crane dimensions and runway interfaces.
    • Hoist, motor, drive and control schedule with electrical diagrams and protection functions.
    • Material and fabrication inspection scope, including specified weld examination and dimensional checks.
    • Factory and site test requirements, acceptance records, manuals and a parts list.

    Define witness points and the records needed at handover. Any required conformity documentation must apply to the ordered equipment and its destination.

    Installation, Commissioning and Maintenance

    Prepare the Installation

    Coordinate delivery with runway readiness, power availability, assembly space and access for lifting equipment. Identify the party responsible for unloading, erection and electrical connections.

    Agree Acceptance

    Define alignment checks, functional tests, protection checks and the applicable load-test scope. Allocate responsibility for test loads, witnessing, records and operator familiarisation.

    Plan Maintenance Access

    Provide safe access and isolation arrangements for hoists, ropes, brakes, wheels and electrical equipment. Follow the supplied manuals and actual duty when setting inspection and lubrication intervals.

    For a production-critical crane, identify essential spares and the space needed to remove components before operation begins. Maintenance access can affect the building layout as well as the crane arrangement.

    Overhead Bridge Crane Price and Supply Scope

    An overhead bridge crane price reflects the load, span, lift, duty, hoist arrangement, controls and supply boundaries. Compare quotations for the same working envelope and operating requirement.

    • Crane equipment: bridge, end carriages, hoist or trolley, controls and agreed protection functions.
    • Runway and power: beams, rails, support steelwork and electrical distribution, as specified.
    • Project services: packing, transport, unloading, installation, commissioning and training scope.
    • Handover requirements: inspection records, manuals, spares, delivery terms and service arrangements.

    When comparing an overhead bridge crane for sale with a hoist or crane kit, check exactly which structures and services are included. Request the selected configuration, exclusions and delivery schedule in the project quotation.

    Request A Bridge Crane Quotation

    Overhead Bridge Crane FAQ

    What is the difference between an overhead crane, bridge crane and EOT crane?

    Overhead crane and bridge crane commonly refer to the same moving-bridge arrangement. EOT means electric overhead travelling and identifies an electrically powered design. The selected bridge, hoist and runway arrangement still need to be specified.

    Should I choose a single-girder or double-girder overhead bridge crane?

    Compare the load, span, highest hook position, duty, runway reactions and installed cost. Double-girder designs allow different trolley arrangements, while a single-girder system may suit general handling. The project layout determines the practical choice.

    Are top-running and underhung cranes different from single- and double-girder cranes?

    Yes. Top running and underhung describe how the bridge travels on its runways. Single and double girder describe the bridge beams. An under-running hoist can be used on a top-running single-girder bridge.

    Can an overhead bridge crane use an existing building?

    It may be possible after the structure and runway are assessed for the proposed crane. Provide building drawings, runway details and condition information. An existing crane’s lifting capacity alone is insufficient to establish compatibility.

    Can the hook reach every part of the crane bay?

    Coverage is limited by side and end approaches, hook height and obstructions. Show each required lifting position on the plan and check both the hook and the suspended load against the proposed crane dimensions.

    Do you offer 5-ton and 10-ton overhead bridge crane configurations?

    The single-girder reference tables include metric 5 t and 10 t examples. Final span, lift, duty and building interfaces need confirmation. Explore the 5 Ton Overhead Crane options or send your full specification for selection.

    What information is needed for an overhead bridge crane quotation?

    Send the required capacity and unit, span, lifting height, runway length, working cycle and power supply. Include load details, the installation country, a building drawing and the required equipment and service scope.

    Request An Overhead Bridge Crane Quote

    Send Henan Mine Crane your load requirement, span, lifting height and operating cycle. Add the building layout, site power supply, installation country and required supply scope so the proposal can address the crane, its working area and its installation interfaces.

    Henan Mine CraneDiscuss your requirements ↗
  • Aircraft Hangar Crane Systems

    Aircraft Hangar Crane Systems

    Aircraft Hangar Crane Systems

    Henan Mine Crane · Aircraft MRO, Engine Handling and Hangar-Wide Maintenance Access

    Aircraft Hangar Crane Systems

    Engineered overhead and underhung crane systems for aircraft maintenance, engine removal and installation, landing-gear service, component replacement, tooling transfer and elevated access across large hangar bays.

    Each aircraft hangar crane is configured around the maintained aircraft fleet, maximum service load, approved lifting interfaces, maintenance sequence, hangar clearances, roof or runway capacity, motion-control requirements and destination compliance framework.

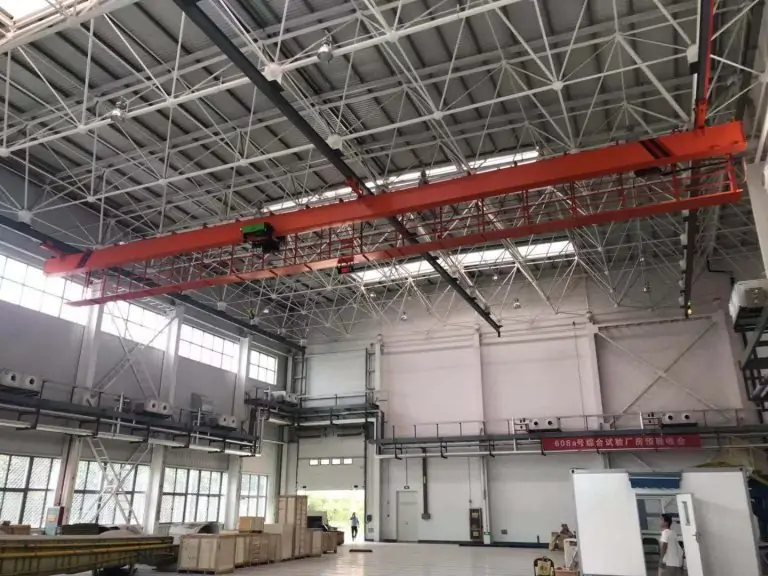
    multi-point suspension crane system arranged for aircraft hangar maintenance
    Large MRO hangars can combine wide-area suspension cranes, service trolleys and synchronized lifting points while preserving aircraft and ground-equipment routes.

    PRIMARY DUTY

    Aircraft Maintenance, Repair and Overhaul

    TYPICAL LOADS

    Engines, Landing Gear, Tooling and Components

    SYSTEM OPTIONS

    Underhung, Bridge, Monorail and Multi-Point

    PROJECT PRIORITIES

    Clear Floor, Low Sway and Aircraft Protection

    What Is an Aircraft Hangar Crane?

    An aircraft hangar crane is an overhead material-handling system designed for maintenance tasks around a complete aircraft. It can lift engines, auxiliary power units, landing gear, flight-control surfaces, cabin modules, maintenance tooling and test equipment, or carry an engineered access platform where the approved maintenance process requires overhead access.

    Hangar work differs from repetitive factory production. Aircraft positions change, several aircraft types may share one bay, mobile stands and docks occupy the floor, tail and wing clearances are restrictive, and the crane may remain lightly loaded for long periods before a critical maintenance lift. Capacity therefore forms only one part of the specification. Coverage, hook approach, low-speed control, collision zoning, component protection, runway reactions and recovery from a control fault are equally important.

    Henan Mine Crane supplies multi-support double-girder underhung cranes, single-girder suspension cranes, double-girder bridge cranes and project-specific multi-hoist systems for new-build and retrofit hangars.

    Aircraft Hangar Crane Applications

    The crane schedule should follow the actual maintenance work package and aircraft fleet. A narrow-body engine-change bay, wide-body heavy-maintenance hangar, military depot, business-jet facility and helicopter maintenance workshop can require different spans, service loads, access arrangements and restricted zones.

    Separate lifting arrangements can be assigned to high-value aircraft components, general tooling and elevated maintenance access so that each duty receives the appropriate control, attachment and inspection regime.

    large-span suspension crane serving an open aircraft maintenance hangar
    Ceiling-supported coverage keeps the hangar floor available for aircraft, docking systems, tugs, stands and maintenance vehicles.

    Engine Removal and Installation

    Controlled vertical movement, accurate lateral positioning and a compatible engine cradle support disconnection, lowering, transfer and reinstallation without uncontrolled sway.

    Landing-Gear Service

    Load control and fine positioning help maintain component orientation during removal, overhaul support, replacement and alignment with approved fixtures.

    Flight-Control and Airframe Parts

    Flaps, rudders, elevators, fairings, doors and structural panels may require long spreaders, protected contact surfaces and several balanced support points.

    Cabin and Interior Modules

    Monorails, light suspension cranes or service hoists can move seats, monuments, galleys, test equipment and maintenance materials along defined routes.

    Maintenance Docks and Tooling

    The crane can reposition calibrated fixtures, engine stands, access-dock sections and maintenance equipment while preserving clear marked routes around the aircraft.

    Overhead Maintenance Access

    A purpose-engineered telescopic platform can provide stable access to upper fuselage, tail and wing areas when platform duty, personnel protection and emergency recovery are included in the system design.

    Aircraft Hangar Crane vs. Aircraft Manufacturing Crane

    Project Factor Aircraft Hangar Crane Aircraft Manufacturing Crane
    Primary Operation Inspection, maintenance, repair, overhaul and component replacement Part fabrication, subassembly, joining and production-line positioning
    Operating Pattern Variable work orders, aircraft types, bay positions and maintenance intervals Defined stations, repeatable load families and production takt
    Typical Equipment Suspension bridges, service trolleys, engine hoists, monorails and teleplatforms Assembly cranes, synchronized multi-hoist systems, process attachments and fixtures
    Layout Priority Flexible coverage around complete aircraft, doors, tails, wings, docks and vehicles Accurate service to fixtures, assembly stations and defined production routes

    Facilities combining final assembly and maintenance can share structural principles, but the load cases, traffic plan, control modes and acceptance tests remain duty-specific. Production applications are covered separately in the aircraft manufacturing crane guide.

    Aircraft Hangar Crane Selection Considerations

    Aircraft Fleet and Work Scope

    Aircraft models, parking positions, maintenance checks, removable components, approved procedures and future fleet changes define the required coverage.

    Rated and Net Hook Load

    The heaviest component, fixture, spreader, sling, powered attachment and credible center-of-gravity position are included in the load schedule.

    Coverage and Hook Approach

    Plan and elevation drawings verify service around the nose, wings, engines and tail, including door pockets, roof trusses, docks and parked equipment.

    Motion Quality

    Low-speed range, acceleration, braking, sway control, travel accuracy and radio-control ergonomics are defined for the most sensitive maintenance task.

    Hangar Structure

    Roof capacity, runway beams, support spacing, deflection, fatigue, connection details, seismic criteria and erection access govern the structural arrangement.

    Maintenance Environment

    Temperature, humidity, washing, coatings, lighting, fire systems, paint or solvent areas and required enclosure protection are documented by bay.

    Aircraft Hangar Crane Configurations Compared

    Configuration Suitable Hangar Duty Operational Value Critical Engineering Check
    Single-Girder Suspension Crane Engine accessories, tooling, cabin modules and general MRO loads Low self-weight, clear floor and efficient coverage below roof steel Roof reactions, hook approach, span and load path
    Multi-Support Double-Girder Underhung Crane Large hangars requiring long spans, broad coverage and higher service loads Load distributed across several support lines with no floor columns Support tolerances, girder deflection and load equalization
    Top-Running Bridge Crane Heavy engine, landing-gear, tooling and facility-maintenance loads Robust lifting platform with defined runway support Column locations, runway elevation, hook approach and wheel loads
    Interlocking Suspension Crane Network Multi-bay MRO with cross-bay transfer of hoists, trolleys or platforms Flexible routing without duplicating every service unit in every bay Bridge alignment, locking logic, transfer interlocks and safe states
    Monorail or Dedicated Service Hoist Repeatable engine route, component shop link or maintenance-equipment transfer Simple controlled route and compact building interface Route geometry, switches, curves, clearance and rescue access
    Synchronized Multi-Hoist System Long or flexible airframe parts, docks and special maintenance fixtures Controlled load sharing, leveling and orientation at several points Point loads, synchronization tolerance, fault response and recovery
    Crane-Mounted Teleplatform Upper-fuselage, wing and tail inspection or repair access Wide elevated access from a movable overhead carrier Personnel-lifting rules, mast stability, collision control and emergency lowering

    Published Multi-Support Hangar Crane Range

    Henan Mine Crane publishes a multi-support double-girder underhung platform for aircraft manufacturing plants and aircraft maintenance hangars. The crane is suspended from several support rails to distribute reactions and preserve an unobstructed floor.

    The ranges below define available product boundaries rather than one standard hangar model. Final ratings, motion speeds, number of supports, clearances and structural reactions are selected from the aircraft maintenance duty and verified building data.

    multi-support double girder underhung crane for a large aircraft hangar
    Several runway support lines can extend coverage across a wide hangar while reducing dependence on floor-mounted crane columns.
    Published Parameter Available Range Hangar Project Input
    Rated Capacity 3–40 t or customized Heaviest component plus all below-the-hook equipment
    Span 10–80 m or customized Bay width, support grid, hangar door and tail clearance
    Lifting Height 6–30 m or customized Aircraft geometry, maintenance stands and required service elevation
    Working Class A3–A5 or customized Load spectrum, starts, travel, shifts and intended service life
    Hoisting Speed 0.5–16 m/min Maintenance cycle and required low-speed positioning range
    Trolley Travel Speed 2–20 m/min Approach zones, sway limits and traffic restrictions
    Crane Travel Speed 5–60 m/min Runway length, zone speeds and stopping distance
    Power Supply 220–690 V, 50/60 Hz Site voltage, earthing, available power and local electrical code
    Published Protection Level IP54 Actual dust, moisture, washing and classified-area requirements

    Engine, Landing-Gear and Multi-Point Handling

    Engine and landing-gear work requires a defined lifting method, not only a hook over the work area. The technical schedule identifies component mass, center of gravity, approved attachment points, fixture deadweight, extraction direction, required orientation and every temporary support state.

    Variable-frequency motions provide controlled acceleration and low-speed adjustment. Load monitoring can identify overload or unequal load share. Where two or more hoists lift one component or fixture, encoder feedback, synchronization limits and a safe fault response keep the points within the permitted relative-height window.

    The aircraft multi-point lifting solution covers hangar maintenance, engine handling, landing-gear work and specialized maintenance tooling.

    extra-long-span suspension crane for aircraft engine and component maintenance
    Fine hoist and travel control support component extraction, transfer and alignment around a parked aircraft.
    Attachment
    Approved fixture, spreader, sling geometry, positive engagement and protected contact surfaces.
    Load Control
    Net hook load, point-load range, overload limit and center-of-gravity envelope.
    Fine Motion
    Defined low speed, acceleration, braking, inching and permissible sway.
    Acceptance
    Representative load, fixture interface, clearance, positioning and recovery tests.

    Service Trolleys, Teleplatforms and Interlocking Crane Networks

    A large MRO facility can use several suspension bridges connected by controlled transfer points. A service trolley or telescopic platform moves along one bridge, the bridges align and lock, and the unit transfers into another bay. This architecture extends maintenance access without assigning a complete duplicate equipment package to every aircraft position.

    Service Trolley

    A hoist trolley supports engines, components and tooling. Capacity, hook approach, power transfer and bridge compatibility are coordinated across every approved route.

    Telescopic Platform

    A rigid telescopic mast can reduce platform sway and reach upper aircraft zones. Rated occupancy, tools, rescue, emergency lowering and personnel-lifting compliance form part of the design basis.

    Bridge Locking and Transfer

    Mechanical alignment, positive locking, position confirmation, motion inhibition and load-state logic prevent transfer until both bridge paths are safely connected.

    Zoned Motion

    Position monitoring can impose slow zones, no-go areas, height limits and defined parking positions around aircraft tails, doors, docks and other cranes.

    Power and Communications

    Busbars, festoons, cable management, radio control and data communications are arranged to avoid snagging and maintain service across transfer interfaces.

    Maintenance and Rescue Access

    Inspection platforms, isolation points, retrieval provisions and manual or powered recovery routes are included for bridges, hoists and personnel-access units.

    Hangar Building, Door and Aircraft-Clearance Integration

    precision aerospace crane integrated with a high-clearance hangar building
    Crane elevation, support points and travel limits are coordinated with the complete hangar section before final structural design.

    Hangar geometry is developed in plan and elevation using the aircraft envelope, towing route, maintenance docks, tail position, wing-tip clearance, hangar doors, roof trusses and all overhead services. The crane must reach the maintenance point without creating a conflict elsewhere in the bay.

    The structural interface schedule states maximum and minimum vertical reactions, transverse and longitudinal forces, buffer loads, simultaneous crane positions, fatigue cycles, support tolerances, runway or roof deflection, seismic actions where applicable, and erection loads. Existing hangars require verified drawings and a condition assessment before support capacity is accepted.

    Lighting, sprinklers, smoke extraction, ventilation ducts, door drives, antennas and maintenance walkways are included in the coordinated model. Isolation access and component-removal routes remain available after the aircraft and docking system occupy the bay.

    Aircraft Protection, Safety Functions and Acceptance

    The control philosophy links each motion to the aircraft protection plan and maintenance method. Safety functions are selected from the risk assessment, destination regulations, crane type and any personnel-lifting duty.

    Protective Functions

    Overload and overtravel protection, emergency stop, motion limits, anti-collision, restricted zones, warning devices, brake supervision where specified and safe electrical isolation.

    Aircraft Surface Protection

    Low-sway travel, padded or approved attachments, controlled approach speed, protected hooks, positive fixture locking and exclusion of loose objects from lifting equipment.

    Factory Acceptance Test

    Mechanisms, controls, alarms, limits, interfaces, simulated faults, load-monitoring functions, synchronized motion and contracted document hold points.

    Site Acceptance Test

    Runway geometry, travel clearances, electrification, rated and proof loads, zone functions, representative routes, accuracy, recovery, training and handover records.

    Maintenance-Task Validation

    Approved fixture engagement, engine or component clearance, low-speed placement, route access and defined abnormal-state recovery are verified with a representative load.

    Lifecycle Records

    Inspection schedules, lifting-accessory records, calibration where required, rope and brake checks, critical spares, software backups, maintenance logs and change control.

    Codes and Standards

    The purchase specification identifies the governing jurisdiction and selected design basis. Applicable references can include ISO 4301-1 for crane classification, ISO 9927-1 for inspections, EN 15011 for bridge and gantry cranes, ASME B30.2 for applicable top-running cranes, ASME B30.17 for applicable underhung cranes and monorails, OSHA 1910.179 for covered United States installations, and IEC 60079 where a formally classified explosive atmosphere exists. Personnel-lifting platforms require a separate compliance and risk-assessment route.

    Wash Areas, Paint Bays and Classified Hangar Zones

    A general maintenance hangar does not automatically require explosion-protected construction. Paint, solvent, fuel-system or battery work may create a classified zone only after the facility’s hazardous-area study defines the substance, zone or division, gas or vapor group, temperature class, ventilation basis and equipment category.

    Where classification is confirmed, motors, brakes, enclosures, controls, cable systems, limit devices and operating procedures are selected for the declared environment. A crane crossing classified and unclassified bays requires clear equipment boundaries and an approved operating philosophy.

    Wash areas and humid coastal hangars can require higher enclosure protection, corrosion-resistant components, compatible coatings, drainage control and a revised inspection schedule. Ambient temperature, altitude and outdoor exposure at the hangar door are included in the equipment data sheet.

    protected double girder bridge crane for a classified aircraft maintenance zone
    Electrical and mechanical protection is selected from the documented hangar environment and governing conformity route.

    Published Aircraft MRO System Reference

    Subang Airport Hangar 3, Malaysia

    A public project announcement dated 6 June 2025 describes an integrated MRO crane package for Hangar 3 at the Subang Airport IVP Complex. The announced supply includes two 500 kg teleplatform units, five suspension crane bridges, two service trolleys rated up to 10 t, crane runways and power-supply lines. Bridge latching mechanisms allow the maintenance units to transfer across bays.

    5 Suspension Bridges
    Overhead coverage distributed across the MRO work area.
    2 Teleplatforms · 500 kg
    Elevated aircraft access carried by the crane network.
    2 Service Trolleys · Up to 10 t
    Component and tooling lifting across approved routes.
    Cross-Bay Transfer
    Bridge locking connects service routes between hangar sections.

    Public industry reference: Subang Airport IVP Complex Hangar 3 project announcement, 2025. The reference illustrates MRO system architecture and is not a Henan Mine Crane delivery record.

    Henan Mine Crane Aerospace Precision-Handling Experience

    Henan Mine Crane aerospace precision handling equipment for a research institute
    Published project imagery shows customized aerospace lifting equipment manufactured for precision component handling.

    24 Equipment Sets for an Aerospace Research Institute

    Henan Mine Crane reports delivering 24 equipment sets to an aerospace research institute, including six lower-rotating girder bridge cranes placed into operation. The published application covers precision transfer of aerospace power components and structural parts.

    The equipment uses PLC and inverter closed-loop vector control, remote, manual and tablet operating modes, and a servo-controlled attachment with extension and rotation. Published performance includes positioning accuracy of ±2 mm and attachment rotation accuracy of ±0.5° for the project configuration.

    The delivery passed acceptance by the Xi’an Institute of Special Equipment Inspection and Testing. This record demonstrates adjacent aerospace precision-handling capability; an aircraft MRO hangar system is engineered from its separate fleet, building and maintenance requirements.

    View Published Aerospace Project →

    Aircraft Hangar Crane Price and Budget Scope

    Public online prices reviewed in 2026 demonstrate the large difference between a bridge kit, a complete freestanding crane and an integrated aircraft-hangar MRO system. A hangar quotation is developed only after the load schedule, coverage, building interface, control functions and contracted services are defined.

    Public Market Reference Published Price Supply Level Scope Boundary
    2 t Bridge Crane Kit US$13,830.51 Gilmore-Kramer online component listing A configurable bridge kit requiring span and running arrangement; not a complete hangar installation
    5 t Crane Kit, 20 ft Span US$22,384–24,322 Starke 2026 price-book configurations Listed kit price varies by festoon, traveling pendant or radio package; runway, erection and hangar integration are separate
    2 t Two-Cell Freestanding Bridge System US$73,487.30 Listed 20 ft × 40 ft-per-cell system Complete commercial configuration; aircraft fixtures, local works and MRO control functions remain separate
    7.5 t Two-Cell Freestanding Bridge System US$94,750.80 Listed 20 ft × 40 ft-per-cell system Fixed retail geometry; aircraft clearances, attachment and acceptance scope are not included
    3 t Three-Cell Freestanding Bridge System US$114,548.05 Listed 30 ft × 90 ft-per-cell system Complete freestanding commercial system; site, freight and aircraft-specific requirements require confirmation
    Aircraft Hangar Underhung or Bridge Crane Project-specific RFQ Engineered crane, runway or roof interface and controls Price follows span, lift, capacity, support structure, duty, destination and installation boundary
    Multi-Bridge, Teleplatform or Synchronized MRO System Project-specific RFQ Integrated hangar process system Requires transfer logic, personnel-access scope, zoning, aircraft interfaces and project acceptance matrix

    Main Cost Drivers

    Coverage and Structure
    Bay dimensions, span, lift, support lines, runway length, headroom and building reinforcement.
    Lifting Equipment
    Capacity, number of hoists, load monitoring, synchronization, attachments and service trolleys.
    MRO Functions
    Interlocking bridges, transfer routes, teleplatforms, restricted zones and aircraft-protection logic.
    Project Services
    Freight, erection, commissioning, load tests, representative-task validation, training and spares.

    Engineering and Procurement Deliverables

    Design Basis

    Aircraft fleet, maintenance tasks, loads, fixtures, duty, environment, standards, operating modes and supply exclusions.

    General Arrangement

    Plan, elevation, aircraft envelope, hook approaches, transfer routes, parking positions, maintenance access and electrification.

    Structural Interface

    Support coordinates, vertical and horizontal reactions, buffers, simultaneous positions, tolerances, deflection and erection loads.

    Control Description

    Speed modes, interlocks, zones, anti-collision, bridge transfer, load monitoring, alarms, communications and recovery logic.

    Inspection and Test Plan

    Manufacturing records, mechanism tests, load tests, safety-function checks, transfer tests, task validation and document hold points.

    Commercial Schedule

    Price, Incoterm, milestones, delivery, site services, acceptance, documentation, training, spares, warranty and exclusions.

    Aircraft Hangar Crane RFQ Data

    RFQ Item Information Required Engineering Use
    Aircraft and Tasks Aircraft types, parking coordinates, maintenance checks and planned lift sequence Coverage, routes, zones and operating modes
    Load Schedule Component masses, dimensions, centers of gravity, lifting points and fixtures Capacity, hoist arrangement and below-the-hook design
    Hangar Drawings Plans, sections, doors, roof steel, columns, docks, services and floor routes Span, lift, hook approach, support layout and collision study
    Structural Data Permitted reactions, support spacing, deflection and existing-building condition Runway, suspension and reinforcement concept
    Performance Duty, motions, speed ranges, synchronization, accuracy and cycle expectations Mechanism class, drives, feedback and controls
    Site Conditions Power, temperature, humidity, altitude, corrosion, dust and hazardous-area classification Electrical and environmental configuration
    Compliance and Supply Destination, governing code, documentation language, Incoterm and site-service scope Conformity route, quotation boundary and project schedule

    A preliminary layout and budget can be prepared from an aircraft envelope, hangar plan, maximum service load and required coverage. A firm quotation requires verified structural interfaces, detailed load cases, agreed controls, destination requirements and a defined installation and acceptance boundary.

    Aircraft Hangar Crane FAQ

    Which crane type is suitable for a large clear-floor hangar?

    A multi-support underhung crane is frequently considered where roof or runway support can carry the required load and floor columns would obstruct aircraft or maintenance traffic. A top-running bridge crane remains practical when dedicated columns and runways are available.

    Can one crane serve several hangar bays?

    Yes. Interlocking suspension bridges can transfer compatible service trolleys or platforms between bays. Bridge alignment, locking, power continuity, transfer interlocks and route clearances must be engineered as one system.

    How is capacity selected for aircraft engine handling?

    Capacity includes the heaviest approved engine or component, cradle, spreader, slings, attachments and applicable dynamic or eccentric load conditions. The maintenance method also defines hook approach, low speed and required orientation.

    Can an aircraft hangar crane carry personnel?

    Only a purpose-engineered personnel-access system should perform that duty. A teleplatform requires its own rated load, fall protection, control hierarchy, collision prevention, emergency lowering, rescue plan and compliance assessment. A standard cargo hook does not establish personnel-lifting suitability.

    Can a crane be installed in an existing aircraft hangar?

    Yes, subject to verified building geometry and structural capacity. Retrofit engineering covers roof or column condition, reactions, reinforcement, access for erection, electrical supply, fire systems and continuing hangar operations.

    Does every hangar require an explosion-proof crane?

    No. Explosion-protected equipment is selected from the formal hazardous-area classification for a specific paint, solvent, fuel or process zone. The general aviation application alone does not determine explosion-protection requirements.

    What determines aircraft hangar crane lead time?

    Engineering approval, structural coordination, customized steelwork, hoists and controls, teleplatform or transfer equipment, conformity documentation, factory testing, ocean freight, site readiness and commissioning all affect the schedule.

    Request an Aircraft Hangar Crane Quote

    Submit the aircraft fleet, maintenance tasks, maximum service load, hangar drawings, required coverage, site power, destination and installation scope for an engineered crane proposal.

    Henan Mine CraneDiscuss your requirements ↗
  • Motorized Gantry Crane

    Motorized Gantry Crane

    Motorized Gantry Crane

    Henan Mine Crane · Powered Gantry Lifting Systems

    Motorized Gantry Crane

    Henan Mine Crane supplies motorized gantry cranes for controlled lifting and material transfer in workshops, fabrication facilities, storage yards and construction sites. Available configurations include rail-mounted single-girder, double-girder and semi-gantry systems engineered for the required load, travel path and operating duty.

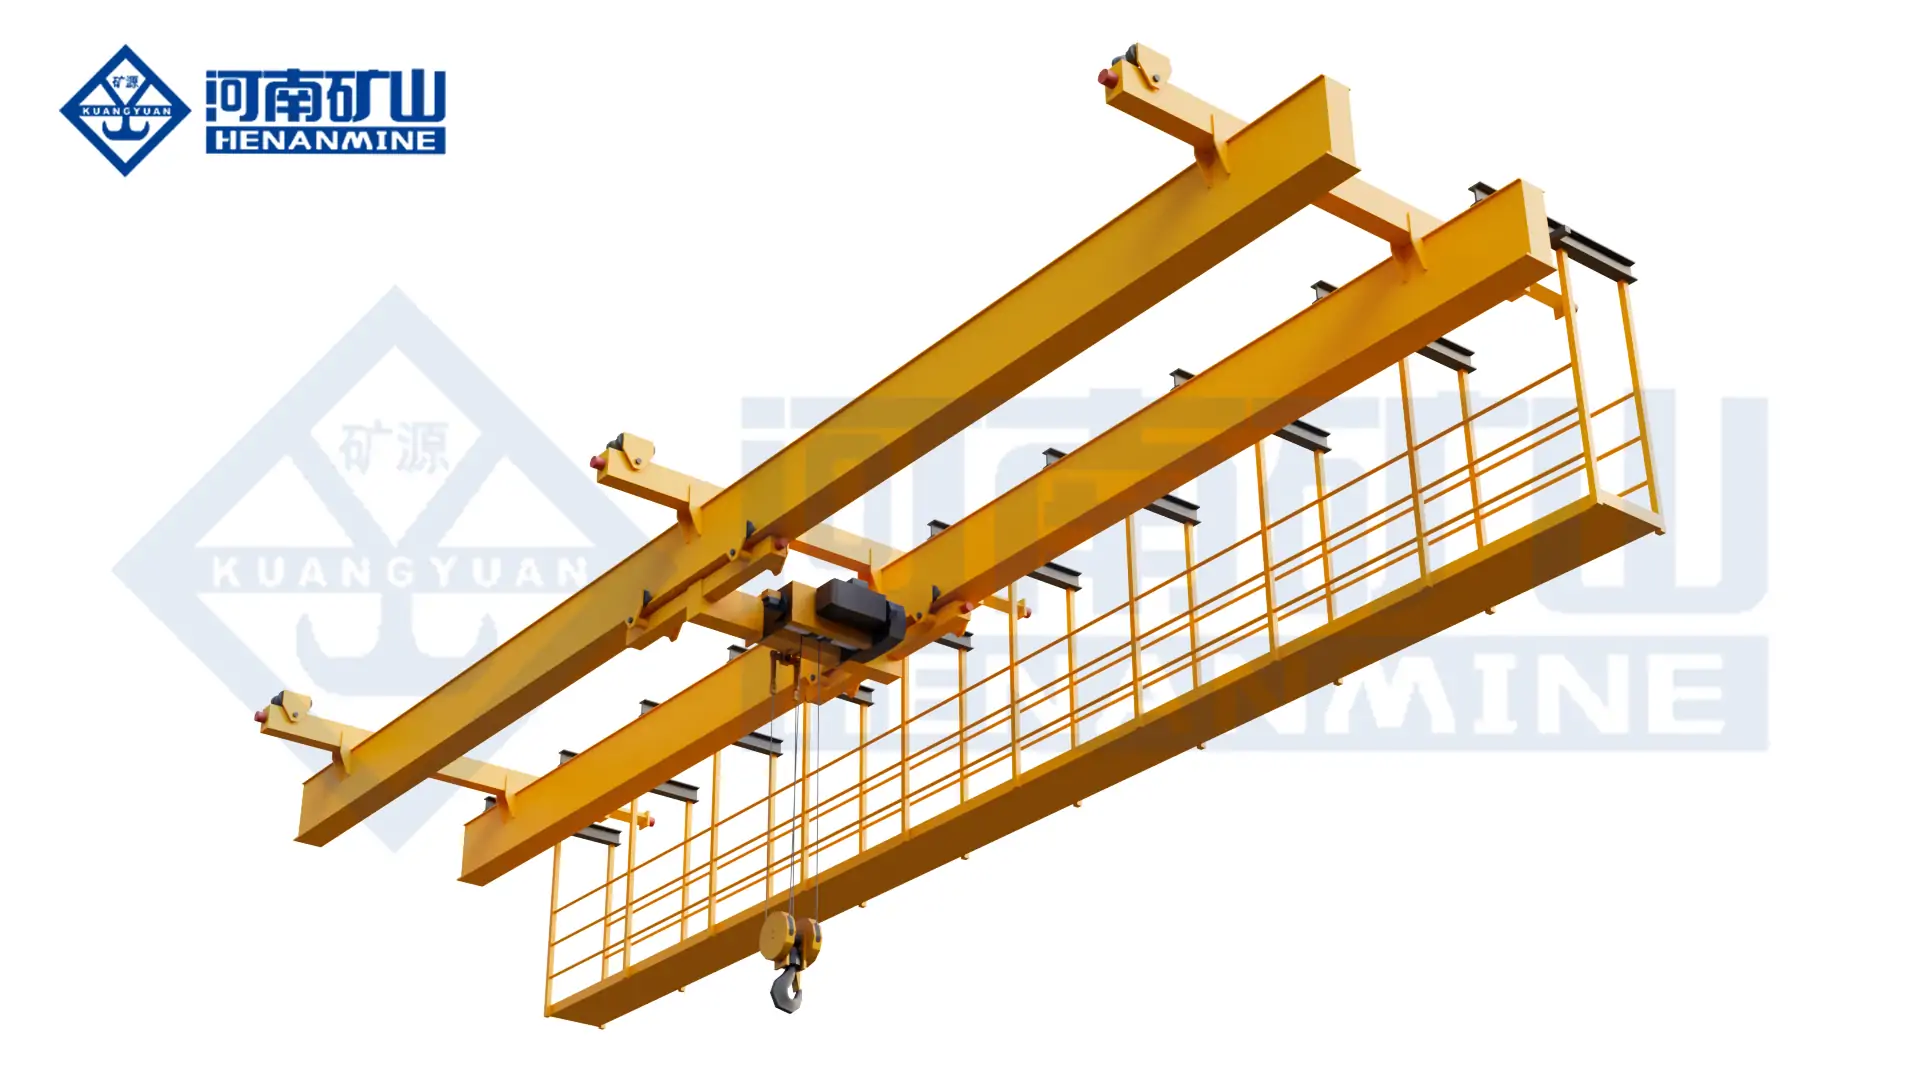
    Industrial single-girder motorized gantry crane with electric hoist and powered rail travel
    Industrial electric-hoist gantry arrangement. Capacity, span, lifting height, travel drives and rail interfaces are selected for the project.

    PRIMARY SCOPE

    Industrial Rail-Mounted Gantry

    POWERED MOTIONS

    Hoist · Trolley · Long Travel

    STRUCTURES

    Full or Semi · Single or Double

    QUOTE INPUTS

    Load · Span · Lift · Duty · Site

    Motorized Gantry Crane Design and Operating Principle

    A gantry crane supports the bridge girder on travelling legs instead of two elevated building runways. The hoisting mechanism provides vertical movement, the trolley provides cross travel, and the complete gantry provides longitudinal travel. Electric drives can be specified for all three motions to achieve controlled material transfer across the required working area.

    The same product term may also refer to a powered mobile workshop gantry operating on floor wheels. Mobile and rail-mounted systems have different requirements for floor condition, steering, stability, capacity, span and loaded travel; they should therefore be specified as separate equipment categories.

    Term Used in an Enquiry Possible Meaning Required Quotation Definition
    Motorized gantry crane Usually a gantry with powered long travel; hoist and trolley may also be electric. Power and speed for every axis, travel guidance, control method and operating limits.
    Electric gantry crane May refer only to an electric hoist on a manually moved frame. Whether gantry travel and trolley travel are manual or powered.
    Powered mobile gantry A self-propelled frame on powered floor wheels, sometimes track-guided. Floor specification, steering path, slope, wheel loads and permission to travel under load.
    Rail-mounted gantry crane An industrial gantry travelling on fixed ground-level rails. Rail gauge, travel length, wheel loads, foundations, skew control and outdoor provisions.

    For free-moving workshop operation, the enquiry should specify a trackless motorized mobile gantry and include the floor specification, travel route, gradient, turning requirements and loaded-travel condition. Rail-mounted industrial systems require separate runway and foundation data.

    Motorized Gantry Crane Applications

    Fabrication and Assembly

    Suitable for transferring frames, machinery, plate assemblies and long fabrications between production, inspection and dispatch positions. Hook coverage and travel clearance are configured for the load orientation throughout the handling route.

    Outdoor Storage Yards

    Provides powered coverage for stock rows, loading lanes and transfer points without imposing crane loads on the building structure. Wind protection, drainage, rail alignment and parking restraints are incorporated into the project design.

    Precast and Construction Areas

    Supports the handling of molds, reinforcement cages, precast components and project modules within a defined working corridor. Access conditions, foundation interfaces and changing site restrictions form part of the selection basis.

    Maintenance and Service Bays

    Provides lifting coverage where elevated building runways are unavailable or unsuitable. A semi-gantry arrangement can also serve a dedicated working strip adjacent to an existing support structure.

    Selection Considerations

    01 / LOAD

    Payload and Attachment

    Required load data comprise the maximum and typical suspended loads, dimensions, center of gravity, lifting points and the mass of slings, lifting beams, grabs, magnets or other attachments.

    02 / COVERAGE

    Span, Lift and Hook Reach

    Required layout data comprise pickup and placement positions, clear width between the legs, rail gauge, travel length, lifting height, hook approaches and cantilever outreach.

    03 / MOTION

    Travel, Speed and Positioning

    Motion requirements include operating speeds, travel distances, stopping accuracy, inching, load-swing control and any requirement for synchronized or variable-frequency travel.

    04 / DUTY

    Cycles and Load Spectrum

    Crane and mechanism duty are selected from lifts per hour, operating shifts, load distribution and total travel. Rated capacity alone does not establish the required duty classification.

    05 / SITE

    Rails, Ground and Obstacles

    Site information should identify the layout, ground or foundation conditions, rail data, obstacles and vehicle or pedestrian routes throughout the moving-leg envelope.

    06 / ENVIRONMENT

    Weather and Process Conditions

    Environmental data should identify wind, rain, temperature, dust, humidity, corrosion and any hazardous-area or hot-material classification. Special operating environments require dedicated protection and compliance measures.

    Motorized Gantry Crane Compared with Other Gantry Configurations

    Alternative configurations should be evaluated against the same rated load, hook coverage, operating duty and supply boundary. Initial equipment cost must be considered together with civil work, floor preparation, electrification, hook access and the suitability of the motion system for the required operating cycle.

    Configuration Motion and Support Application Fit Critical Procurement Criteria
    Industrial Single-Girder Motorized Gantry Electric hoist and trolley with powered long travel on two ground rails. General industrial handling where the hoist layout meets the required span, lift and duty. Usable hook height, hoist headroom, wheel loads and long-travel control.
    Industrial Double-Girder Motorized Gantry Powered trolley or winch trolley on two girders; powered ground-rail travel. Projects needing another lifting envelope, mechanism arrangement, capacity or duty. Trolley arrangement, maintenance access, total mass, wheel loads and installed scope.
    Motorized Semi-Gantry One ground-travelling leg and one elevated runway end carriage. A working strip beside a suitable building runway or independent elevated support. Compatibility, alignment and drive coordination between the elevated and ground runways.
    Trackless Motorized Mobile Gantry Powered floor wheels guide a portable frame without fixed crane rails. Indoor routes with smooth, sufficiently level floors and a defined steering envelope. Model-specific floor limits, traction, steering, stability and loaded-travel instructions.
    Manual Portable Gantry The frame is moved manually; the hoist may be manual or electric. Occasional local lifting where travel frequency and required manual force remain within the equipment specification. Loaded travel is permitted only where expressly included in the approved model specification and operating instructions.
    Container RMG or RTG Purpose-built rail- or rubber-tyred container handling with a spreader. Container terminals and intermodal yards, not general workshop hook handling. Container stack geometry, spreader duty, automation and terminal operating system interfaces.

    Motorized Gantry Crane Specifications

    The motorized gantry crane specification is developed from the required lifting capacity, geometry, operating cycle, control functions and site interfaces. The approved technical schedule defines the complete lifting system rather than capacity and span alone.

    Parameter Project Definition
    Rated lifting capacity Maximum suspended load and how below-the-hook attachments are included.
    Structure Single girder, double girder, full gantry, semi-gantry, L-type or another engineered arrangement.
    Span and rail gauge Dimensions defined consistently on the general arrangement drawing.
    Lifting height and headroom Required hook position, available total height and clearance above the load.
    Travel length and cantilevers Runway length, end approaches and hook reach inside or outside the legs.
    Crane and mechanism duty Classification selected from working cycles, load spectrum, travel and service conditions.
    Powered axes and speeds Hoisting, trolley travel and gantry travel speeds, ratios and variable-speed requirements.
    Control method Pendant, radio remote, cab, local service controls or an agreed combination.
    Electrical supply Available voltage, phases, frequency, earthing system and allowable supply route.
    Runway interface Rail profile, wheel loads, wheel spacing, horizontal forces, end stops and foundation responsibility.
    Environment Indoor or outdoor conditions, temperature, wind, precipitation, dust, corrosion and formal area classification.
    Applicable requirements Destination-country law, agreed crane and electrical standards, inspection, testing and documentation requirements.

    Available Motorized Gantry Crane Configurations

    Henan Mine Crane provides single-girder, double-girder electric-hoist and heavy-duty double-girder configurations for different capacities, spans, lifting heights and operating classes. Final model selection is based on the complete combination of load, duty, hook coverage, environment and site interfaces.

    Product Family Capacity Range Span Range Lifting Height Work Class
    European Single-Girder Gantry Crane 1–32 t or customized 6–35 m or customized 4–20 m or customized A3–A5
    Double-Girder Electric-Hoist Gantry Crane 3–50 t or customized 7.5–35 m or customized 4–30 m or customized A3–A5
    MG Double-Girder Gantry Crane 5–500 t or customized 8–40 m or customized 6–30 m or customized A3–A8

    The final technical schedule confirms the selected capacity, span, lifting height, work class, mechanism arrangement, overall dimensions and transport conditions for the project.

    Motorized Gantry Crane Motion System

    VERTICAL AXIS

    Electric Hoisting

    The hoist or winch raises and lowers the load through the specified lifting medium and hook or attachment. Capacity, lift, duty, speed, reeving and braking are selected together.

    CROSS AXIS

    Powered Trolley Travel

    The trolley moves the suspended load across the bridge. End approaches, acceleration and positioning affect usable coverage and load control near the legs and cantilevers.

    LONG AXIS

    Motorized Gantry Travel

    Powered end carriages move the complete structure along rails or an approved floor path. Drive coordination, wheel guidance, braking and skew control are essential system decisions.

    Variable-frequency control can provide smoother acceleration, deceleration and low-speed positioning when included in the specification. It does not remove the need to define braking, travel limits, operator visibility and the permitted load-swing envelope.

    Rails, Foundations and Travel Control

    Runway Geometry

    Rail gauge, straightness, level, elevation difference and end alignment affect wheel contact and skew. Inspection and acceptance criteria should be agreed before crane erection.

    Civil and Structural Interface

    Foundation design requires the selected crane’s wheel loads, wheel spacing and horizontal or exceptional forces. Generic capacity alone is not enough for civil design.

    Drive Coordination

    The long-travel design coordinates driven wheels, brakes, acceleration and feedback or correction as required. The aim is controlled travel without excessive skew or flange forces.

    End and Parking Positions

    Define buffers, end stops, travel limits, service access and the normal parking location. Outdoor systems may require rail clamps, anchors or other wind restraints.

    Power Supply, Controls and Safety Functions

    Define the Electrical Boundary

    Record the site voltage, frequency, phases, earthing arrangement and available fault information. The contract should state who supplies the incoming isolator, feeder, runway electrification, trailing cable management and connections.

    • Cable reel, festoon or conductor system selected for travel length and environment.
    • Pendant, radio control, cab or combined operating stations.
    • Single-speed, two-speed or variable-frequency motion as specified.
    • Required enclosure, heating, cooling or corrosion protection.

    Safety and Protective Functions

    • Overload protection and hoisting upper and lower limits as applicable.
    • Service and holding brakes for the selected mechanisms.
    • Trolley and gantry travel limits, buffers and end stops.
    • Emergency stops, isolating provisions and electrical protections.
    • Audible or visual travel warnings and anti-collision functions where required by the risk assessment.

    Applicable design, electrical, inspection and workplace requirements shall be defined according to the destination country and contract. Where required, the technical proposal can be prepared around specified ISO, FEM, EN, CMAA, ASME or national requirements, subject to confirmation of the exact compliance and documentation scope.

    Outdoor Operation and Wind Protection

    Outdoor motorized gantry cranes require project-specific wind, temperature, rain, dust and corrosion data before structural and electrical configuration. Environmental protection, operating limits and parking restraints are incorporated during the design stage.

    Operating and Out-of-Service Wind

    The project specification defines design wind data, operating limits, monitoring, shutdown actions and the secured out-of-service condition.

    Parking and Restraint

    Travel brakes, rail clamps, storm anchors or other restraints are selected from the design and site. Civil interfaces must be coordinated with the foundation scope.

    Weather and Corrosion

    The protection package may include a specified coating system, weather-rated enclosures, drainage, covers and heaters based on rain, dust, humidity, coastal exposure or process chemicals.

    Motorized Gantry Crane Price

    Motorized gantry crane pricing depends on the travel system, lifting capacity, span, lifting height, work class, control method and operating environment. The following ranges are suitable for preliminary capital budgeting; the final commercial offer is prepared against the confirmed technical specification and delivery scope.

    Configuration Operating Arrangement Indicative Equipment Budget Commercial Scope
    Powered Mobile Workshop Gantry Motor-driven floor wheels for flexible movement within a defined indoor route. From approximately €20,000 Final scope depends on capacity, span, powered motions, steering system, controls and permitted loaded travel.
    Industrial Single-Girder Gantry Crane Powered hoisting, trolley travel and rail-mounted gantry travel for general industrial handling. Approximately $10,000–$50,000 Normally quoted as crane equipment; rails, foundations, incoming power, freight and installation require confirmation.
    Industrial Double-Girder Gantry Crane Double-girder bridge with electric-hoist or winch trolley for higher capacity, duty or lifting-envelope requirements. Approximately $30,000–$90,000 Price varies materially with capacity, span, work class, trolley design, access provisions and outdoor protection.
    Complete Installed System Crane equipment integrated with the agreed runway, power, installation and commissioning scope. Project quotation required Commercial offer to define Incoterm, freight, insurance, duties, unloading, erection, testing, training and spare parts.

    Budget ranges do not represent a fixed selling price. Comparable quotations require identical capacity, span, lift, duty, controls, environmental protection and supply boundaries.

    Total Installed Cost Components

    Crane Equipment

    Bridge, legs, hoist or trolley, travel drives, controls and specified protection.

    Rails and Foundations

    Runway steel, civil work, end stops, anchors, alignment and drainage.

    Electrical Interface

    Incoming feeder, isolator, conductor or cable reel, earthing and site connections.

    Delivery and Site Work

    Packing, freight, insurance, duties, unloading, erection, testing and handover.

    Information Required for an Accurate Quote

    1. Load: maximum and typical payload, attachment mass, dimensions and lifting points.
    2. Geometry: span or clear width, lifting height, travel length, approaches and cantilevers.
    3. Operation: lifts per hour, shifts, travel distances, speeds and positioning needs.
    4. Site: layout, rail or floor information, obstacles, traffic, ground and foundations.
    1. Environment: indoor or outdoor, wind, temperature, rain, dust, corrosion and classifications.
    2. Power: voltage, phases, frequency and preferred supply route and controls.
    3. Destination: country, applicable requirements, documentation and inspection plan.
    4. Commercial scope: Incoterm, freight, rails, erection, commissioning, training and spares.

    Commercial evaluation should be based on a common technical specification and an itemized inclusion schedule. The comparison should cover the complete installed system, operating duty and contractual responsibilities rather than the headline equipment price alone.

    Manufacturing and Project Documentation

    Crane structures and equipment in a Henan Mine Crane manufacturing workshop
    Structural fabrication and crane assembly at a Henan Mine Crane manufacturing facility.

    Henan Mine Crane manufactures the structural assemblies and integrates the hoisting, travel, control and electrical systems in accordance with the approved project specification. The documentation package can include the following records within the agreed supply scope. Henan Mine Crane Manufacturing Facilities.

    • General arrangement drawing with dimensions, clearances, hook coverage and service access.
    • Wheel loads, wheel spacing and rail-interface data for civil and structural coordination.
    • Motor and component schedule plus electrical diagrams and control description.
    • Agreed material, welding, inspection, factory test and site acceptance records.
    • Operating, inspection and maintenance manuals with spare-parts identification.

    The contract documentation defines the final technical parameters, component scope, applicable requirements, inspection plan, acceptance criteria and responsibilities for delivery, installation and commissioning.

    Installation, Commissioning and Maintenance

    Site Preparation

    Site preparation includes approved foundations, rails, end stops, power routing, earthing and drainage, together with verification of geometry and installation readiness before equipment delivery.

    Erection and Commissioning

    The installation plan defines unloading and assembly areas, erection equipment, inspection stages, functional checks, applicable load tests, training and handover responsibilities.

    Lifecycle Maintenance

    Safe maintenance access is required for the hoist, trolley, wheels, drives, brakes and electrification. Inspection intervals are established from operating duty, environment, supplied manuals and local requirements.

    Maintenance planning should include rail condition, wheel wear, drive alignment, brake performance, fasteners, wire rope or chain, power-supply wear and outdoor restraint equipment. Record defects and corrective work against the crane’s operating history.

    Motorized Gantry Crane FAQ

    What does “motorized” mean on a gantry crane?

    In most industrial specifications, “motorized” denotes powered gantry long travel; hoisting and trolley travel may also be electrically driven. A complete proposal defines the drive, speed and control method for each motion axis.

    Can a motorized gantry crane move while carrying a load?

    Loaded travel is permitted only where the approved crane design, runway or floor, operating instructions and site procedure support that operating condition. Selection data must define the transported load, hook position, travel route and required loaded-travel cycle.

    Is rail-mounted travel required?

    Industrial gantry cranes commonly operate on fixed rails. Powered mobile workshop gantries can operate on floor wheels, subject to model-specific requirements for floor flatness, slope, traction, steering and stability. The selected travel concept forms part of the approved technical specification.

    Which configuration is appropriate: single-girder or double-girder?

    Configuration selection is based on capacity, span, usable hook height, operating duty, trolley arrangement, maintenance access, wheel loads and total installed cost. Girder quantity alone does not determine crane duty or quality.

    How much does a motorized gantry crane cost?

    A powered mobile workshop gantry may start from approximately €20,000. Industrial rail-mounted single-girder systems may require an equipment budget of approximately $10,000–$50,000, while double-girder systems may range from approximately $30,000–$90,000. Final pricing depends on capacity, span, lifting height, duty, controls, rails, foundations, freight and installation scope.

    Can the crane operate outdoors?

    Outdoor operation is available where the approved design incorporates the specified wind, precipitation, temperature, corrosion and parking conditions. The protection package can include weather-rated electrical equipment, protective coatings, wind monitoring and restraint systems.

    What power supply does a motorized gantry crane use?

    The electrical system is configured for the destination supply and the selected motors and controls. Required electrical data include voltage, phases, frequency, earthing arrangement and travel length for definition of the feeder and mobile electrification system.

    Is a motorized gantry crane the same as an overhead bridge crane?

    The two systems use different support arrangements. A full gantry transfers bridge loads through travelling legs to ground-level runways, whereas an overhead crane travels on two elevated runways and preserves floor space without moving legs. Selection depends on building support, foundation work, headroom and site traffic routes.

    Can an existing runway be reused?

    Reuse is assessed after surveying rail geometry, condition and supporting foundations. The proposed crane may have different wheel loads, wheel spacing, horizontal forces or electrical demand from the previous system.

    What information is required for a quotation?

    Quotation data should include the load, span, lifting height, travel length, cantilevers, operating cycle, site drawing, environmental conditions, electrical supply, project location and required freight, rail, installation and commissioning scope.

    Request A Motorized Gantry Crane Quote

    Henan Mine Crane prepares project-specific proposals based on the required load, span, lifting height, travel length, operating duty, site layout, environment and electrical supply. The proposal can compare suitable full-gantry, semi-gantry, single-girder and double-girder arrangements and define the powered motion package.

    The requested commercial scope should identify responsibility for rails, foundation interface data, freight, installation, commissioning, operator training and recommended spare parts.

    Henan Mine CraneDiscuss your requirements ↗
  • Metal Recycling Crane Systems

    Metal Recycling Crane Systems

    Metal Recycling Crane Systems

    Henan Mine Crane · Scrap Yard and Recycling Process Handling

    Metal Recycling Crane Systems

    Heavy-duty overhead and gantry cranes for scrap receiving, sorting, stockpiling, shear and shredder feeding, baler service, processed-metal transfer and dispatch.

    Henan Mine Crane engineers each metal recycling crane around the actual scrap mix, attachment deadweight, representative pick mass, pile geometry, cycle rate, duty class, operating environment, safety zones, plant interfaces and contracted supply boundary.

    electromagnetic bridge crane platform for ferrous metal recycling service
    A metal recycling crane may use an electromagnet, orange-peel grab, mechanical lifting device or hook, selected from the verified material stream and operating sequence.

    PRIMARY SERVICE

    Scrap Receiving, Sorting and Feeding

    CRANE ARCHITECTURE

    Overhead or Gantry Crane

    LIFTING DEVICES

    Magnet, Orange-Peel Grab or Hook

    CONTROL LEVELS

    Cabin, Radio, Assisted or Automatic

    What Is a Metal Recycling Crane?

    A metal recycling crane is an overhead travelling crane or gantry crane configured to move ferrous scrap, nonferrous scrap, mixed metal, bales, bundles, chips and process equipment within a recycling facility. Typical duties include unloading incoming material, building and reclaiming stockpiles, sorting grades, feeding a shear, shredder, baler or furnace, moving processed material and loading trucks, rail wagons or containers.

    The crane is a handling system rather than a catalog bridge fitted with any available attachment. Scrap shape, magnetic response, density, entanglement, contamination, temperature and pile condition determine the lifting device. The chosen magnet or grab then affects crane capacity, hoist reeving, power supply, control logic, cycle time, wheel loads and maintenance access.

    Henan Mine Crane develops recycling systems from electromagnetic bridge crane, grab overhead crane, grab-and-hook crane and project-specific gantry crane platforms.

    Metal Recycling Material-Handling Flow

    A procurement specification begins with every source, destination and abnormal route. Different zones can require different attachments or separate cranes even when the nominal load appears similar.

    1. Receiving and Inspection

    Unload trucks, rail wagons, containers or transfer bins into an inspection area. The receiving plan covers vehicle clearances, unloading sequence, traffic separation and quarantine of closed vessels, batteries, cylinders, hot material or other rejected items.

    2. Sorting and Segregation

    Separate ferrous and nonferrous grades, oversize pieces, turnings, plate offcuts, castings and contaminants. Magnetic pickup can support ferrous segregation; mixed or nonmagnetic streams normally require a suitable mechanical grab.

    3. Stockpile and Reclaim

    Build controlled piles and reclaim material without exceeding floor, retaining-wall, bin or crane-envelope limits. Pile height, slope, buried dense pieces and interlocked scrap affect penetration, pickup stability and cycle time.

    4. Process-Line Feeding

    Feed a shear, shredder, baler, crusher, sorting line, conveyor hopper or furnace charge system at a controlled rate. Equipment-ready signals, hopper level, gates, safe approach and release permissives are included in the control sequence.

    5. Processed-Metal Transfer

    Move shredded scrap, cut scrap, compacted bales, bundles or chips to inspection, storage or blending positions. Product form may require a closed grab, magnet, bale clamp, lifting beam or conventional hook rigging.

    6. Dispatch and Maintenance

    Load outbound vehicles and support planned maintenance of magnets, grabs, shredders, balers and conveyors. Production handling and maintenance lifts are documented separately, with defined attachment changeover and parking arrangements.

    electromagnetic overhead crane platform used for ferrous material handling
    The handling study records material routes, traffic lanes, pile limits, process interfaces, attachment parking and recovery positions before crane selection.

    Metal Recycling Crane System Architecture

    Bridge or Gantry Structure

    Top-running double-girder cranes suit fixed indoor bays. Gantry cranes serve open yards where a building runway is unavailable. Structure, wheels and drives are calculated from span, fatigue spectrum, skewing, wind and maximum wheel reactions.

    Process-Duty Hoisting Machinery

    Drum, ropes, sheaves, reducer, motor, brakes and controls are sized for gross suspended load, lifting height, starts per hour, load spectrum, shock and required availability rather than rated tonnage alone.

    Scrap Attachment

    An electromagnet, orange-peel grab, closed multi-tine grab, bale device, lifting beam or hook is matched to representative material. Attachment mass and service connections remain part of the rated suspended load.

    Attachment Power and Protection

    Magnet rectifiers, cable reels and retention provisions, or hydraulic power packs, hoses and rotators, are guarded against sharp scrap, impact, abrasion, heat, dust, rain and accidental snagging.

    Operator and Control System

    Cabin, radio control, assisted functions or automatic operation can include cameras, load display, anti-sway, position tracking, pile profiling, destination confirmation and process-line handshakes.

    Access and Maintainability

    Walkways, service platforms, guarded access, isolation stations, attachment stands and component-removal paths reduce maintenance exposure above stockpiles and operating equipment.

    published double girder grab crane platform for heavy material handling
    Published Henan Mine Crane grab-crane architecture illustrates the bridge, hoist, attachment and control platform; a scrap-rated orange-peel grab remains a project-specific selection.

    Metal Recycling Crane Selection Considerations

    A reliable selection separates the crane rating, net scrap payload and realistic production throughput. The following inputs define the starting design basis.

    Scrap Composition

    Ferrous percentage, nonferrous grades, piece dimensions, shape, entanglement, density, coatings, contamination, temperature and seasonal variation are recorded from representative loads.

    Attachment and Net Payload

    Magnet, grab, rotator, hook block, beam, cables and hoses consume part of the crane rating. Net scrap payload is calculated after every suspended component is included.

    Production Throughput

    Required tonnes per hour, average verified pickup, full travel path, hoisting heights, destination queues, attachment closing time and operating availability establish the real cycle requirement.

    Duty and Load Spectrum

    Lifts per hour, shifts, annual hours, average and maximum loads, starts, reversing, impact and production consequence of downtime determine mechanism and structural classification.

    Site and Environment

    Indoor or outdoor location, temperature, wind, rain, snow, dust, metal fines, salt, fumes, washdown, fire exposure and corrosive contaminants determine protection and component placement.

    Layout and Interfaces

    Span, lift, runway length, pile limits, vehicle lanes, process openings, attachment envelope, power supply, plant PLC and maintenance access are verified on coordinated drawings.

    Metal Recycling Crane Configurations Compared

    Configuration Typical Material Principal Strength Key Design Check
    Electromagnetic Overhead Crane Validated ferromagnetic loose scrap, plate offcuts and steel pieces Fast pickup and release without mechanical closure Representative pickup testing, derating, power-loss retention and exclusion zone
    Orange-Peel Grab Overhead Crane Mixed, nonferrous, bulky, irregular or interlocking scrap Mechanical capture across varied material shapes Grab volume, filling factor, penetration, closure force, wear and hose or cable protection
    Metal Recycling Gantry Crane Outdoor yard scrap handled by magnet, grab or hook Large yard coverage without a full building runway Wind, storm securing, ground rail, drainage, corrosion and vehicle segregation
    Hook and Grab or Magnet Crane Scrap plus bales, bundles, bins and maintenance loads Multiple duties from one crane platform Changeover time, parked attachment, connection method, retained rating and recovery procedure
    Automatic Scrap Handling Crane Repeatable stockpile, bunker, hopper and process-line routes Consistent task execution and plant-data integration Pile sensing, destination state, traffic control, abnormal recovery and maintained safe zones
    Configuration rule: an electromagnet is not a universal scrap attachment, and a standard clamshell bulk grab is not automatically suitable for interlocking scrap. Material trials and an approved attachment data sheet establish the working configuration.

    Magnet, Orange-Peel Grab or Hook?

    electromagnetic crane lifting device platform for ferrous scrap handling

    Electromagnet for Verified Ferrous Scrap

    An electromagnet supports rapid handling where the stream is ferromagnetic and the pickup behavior is proven. Capacity depends on magnetic properties, piece thickness, surface contact, air gaps, rust, scale, pile depth, geometry, temperature and how the pieces bridge beneath the magnet.

    A catalog value established on a clean test plate is not the net capacity for random loose scrap. Representative material tests, operating derating, magnet duty cycle, cable management, backup or retention strategy, residual magnetism and controlled release are specified before acceptance.

    published grab overhead crane platform requiring a scrap-specific multi-tine grab

    Orange-Peel Grab for Mixed and Irregular Scrap

    A multi-tine orange-peel grab mechanically captures mixed, nonferrous, bulky and irregular material. Open tines suit bulky scrap, semi-closed tines suit many mixed or sheared streams, and closed tine arrangements can retain smaller pieces or chips.

    Selection covers tine count and profile, open and closed diameter, volume, deadweight, closure force, penetration, rotation, hydraulic or rope actuation, replaceable wear parts, edge protection and expected filling factor for each scrap family.

    Hook, Beam or Bale Device

    Compacted bales, bundled stock, bins and maintenance loads may require certified slings, a lifting beam, tongs, clamps or a conventional hook. Defined lifting points and stable load geometry remain essential.

    Standard Bulk Grab Boundary

    A clamshell or four-rope bulk grab designed for ore, coal, slag or other free-flowing material is not presumed suitable for tangled scrap. Structural loads, closure method and shell geometry require separate confirmation.

    Multiple Attachments

    A dual-purpose crane is practical where attachment exchange frequency, connection safety, parked-attachment location, production interruption and loss of net payload are acceptable within the operating plan.

    Capacity, Grab Volume and Throughput

    Gross Suspended Load

    Crane rated capacity must cover the maximum net scrap mass plus the complete suspended attachment, hook block, rotator, beam, cables and other equipment below the hoist. A crane labeled 20 t does not provide a 20 t scrap payload when a heavy grab or magnet is installed.

    Volumetric Grab Check

    Expected scrap mass per grab is estimated from usable grab volume multiplied by representative bulk density and a verified filling factor, then limited by crane and attachment ratings. Density can change sharply between light-gauge tangled scrap, shredded material, cast pieces and compacted feed.

    Production Cycle Check

    Throughput is calculated from the complete cycle: approach, penetration or magnet placement, closure or energization, hoist, travel, destination wait, lowering, release and return. Average production pickup and availability—not only theoretical maximum load—control tonnes per hour.

    Capacity Data Required

    • Maximum and typical piece mass and dimensions
    • Representative loose bulk density by scrap family
    • Attachment self-weight, services and rotating equipment
    • Measured or trial-based magnet pickup or grab filling factor
    • Source and destination coordinates and lift heights
    • Required tonnes per hour and peak queue condition
    • Daily shifts, annual hours and production availability target
    Procurement check: net payload, average pickup and hourly throughput are three different values. All three must appear in the technical proposal with the assumptions used to calculate them.

    Duty Classification, Controls and Automation

    Load Spectrum and Starts

    Frequent reversals, high starts per hour, variable loads, impact, grab closure and abrupt magnet release create a fatigue profile different from occasional workshop lifting. ISO, FEM or CMAA classification is selected from the declared service.

    Operator Visibility

    A cabin, radio station or remote control room is arranged around pile height, dust, glare and blind spots. Cameras can cover the attachment, hopper, vehicles and travel path but do not replace defined exclusion controls.

    Assisted Functions

    Anti-sway, slow zones, protected travel corridors, height limits, load weighing, position display, grab or magnet status and destination confirmation support repeatable operation.

    Automatic Stockpile Handling

    Position tracking and pile profiling can generate source coordinates and prevent excessive pile height. Automatic release remains inhibited until the destination and process state are confirmed.

    Process-Line Interface

    Signals with shears, shredders, balers, conveyors, bunkers and gates define ready, hold, fault, occupancy, level, release and task-complete states. Ownership of every safety permissive is documented.

    Recovery and Diagnostics

    Safe manual recovery covers failed sensors, incomplete closure, lost magnet feedback, blocked destinations, communications loss and interrupted power. Diagnostics retain events, loads, cycles, alarms and maintenance counters.

    published intelligent grab crane control platform for automated material transfer
    Automation scope is defined by the actual pile, process-line handshake, safety architecture and abnormal recovery method.

    Recycling-Yard Environment and Safety Controls

    Dropped-Material Zone

    Suspended scrap can shift, detach or project beyond the attachment. Personnel routes, vehicle routes, operating stations and maintenance access are separated from the defined load path and release zone.

    Incoming-Scrap Hazards

    Batteries, sealed containers, cylinders, residual fluids, hot pieces, radioactive sources and unknown chemicals require receiving inspection, rejection and quarantine procedures. Crane selection does not replace material acceptance controls.

    Fire and Emergency State

    Fire detection, evacuation, emergency stops, safe parking and response to a retained suspended load are coordinated with the site emergency plan. Battery-containing scrap and hot loads receive specific controls.

    Dust, Fines and Abrasion

    Sealed enclosures, filtered or pressurized electrical rooms, guarded cables, abrasion-resistant liners, protected sensors and accessible cleaning points are selected from the measured environment.

    Outdoor Operation

    Wind monitoring, operating and out-of-service wind limits, rail clamps or storm anchors, drainage, low-temperature provisions, lightning protection and corrosion systems are established for the site.

    Hazardous-Area Boundary

    Explosion-protected equipment is specified only where a formal area classification identifies combustible gas or dust zones. General metal dust or a recycling application name alone does not establish an ATEX or IECEx scope.

    Operating boundary: no person is permitted beneath suspended scrap. Administrative rules, physical segregation, warning systems and control functions are coordinated to keep people and vehicles outside the load path.

    Runway, Yard and Maintainability Interfaces

    Existing Runway Verification

    Reuse requires condition and geometry checks of rails, beams, brackets, columns, connections and foundations. Maximum and minimum wheel loads, lateral and longitudinal forces, buffer reactions and fatigue demand are issued for structural review.

    Stockpile and Clearance Model

    The model includes maximum pile contours, protruding pieces, attachment swing or rotation, hopper edges, vehicle envelopes, lighting, ductwork, columns and adjacent cranes. Storage rules prevent stockpiles from entering a protected motion envelope.

    Wear and Service Access

    High-wear tines, shells, magnet chains, cable outlets, hoses, sheaves, wheels and brakes remain inspectable. Attachment stands, safe parking, washdown or cleaning provisions and component-removal paths are defined before fabrication.

    Site Documents

    • Verified bay, runway and yard drawings
    • Allowable wheel reactions and foundation information
    • Pile, bin, hopper, building and vehicle envelopes
    • Rail condition, elevation, span and alignment survey
    • Power, grounding, communications and fire-system interfaces
    • Erection opening, laydown area and shutdown window
    • Environmental and hazardous-area assessments
    double girder grab crane installation considered in runway and maintenance planning
    Crane, runway, stockpile, process equipment, attachment service connections and maintenance access form one engineered operating envelope.

    Applicable Standards and Acceptance Testing

    The purchase specification identifies the governing jurisdiction, crane design standard, electrical requirements and rules for lifting magnets or below-the-hook devices. Common reference frameworks include ISO 4301 for classification, ISO 9927 for inspections and ISO 12480-1 for safe use; EN 13001 and EN 15011; CMAA 70 and ASME B30.2; and ASME B30.20 with ASME BTH-1 where applicable to the lifting device.

    IEC 60204-32 can govern electrical equipment for hoisting machines; ISO 13849-1 or IEC 62061 can inform safety-related control functions; IEC 60529 addresses enclosure ingress protection; and ISO 12944 can inform protective coating selection. IEC 60079, ATEX or IECEx requirements apply only when the approved hazardous-area classification establishes that scope. Local law and the signed contract remain controlling.

    Design Review

    Confirm load cases, classification, gross and net capacities, wheel loads, attachment envelope, material assumptions, protection package, safety functions, interfaces and inspection access.

    Factory Acceptance Test

    Verify assemblies, drives, brakes, limits, load protection, magnet or grab logic, alarms, safety functions, interface simulation, documentation and contracted quality records before shipment.

    Site and Production Acceptance

    Test proof loads, representative scrap, pickup retention and release, grab closure, cycle time, hopper interfaces, collision zones, power-loss response, cameras, positioning and abnormal recovery.

    Acceptance criterion: a proof-load test validates structural and mechanism requirements but does not alone prove scrap-handling performance. Representative material trials and the agreed production cycle remain separate acceptance items.

    Published Adjacent Magnetic-Handling Reference

    Henan Mine Crane published rotating electromagnetic beam crane reference
    Published electromagnetic beam-crane project imagery demonstrates adjacent steel-handling engineering, manufacturing and control capability.

    Automatic Rotating Electromagnetic Beam Platform

    Henan Mine Crane publishes an electromagnetic beam platform with automatic handling functions for steel products and describes a 5–50 t configurable capacity range for the solution family. Positioning, magnetic control and plant interfaces provide relevant engineering experience for ferrous-material handling.

    Evidence boundary: the published benchmark project is identified as slab transfer at a steel base, not as a delivered metal recycling yard crane. Random scrap requires a different magnet arrangement, load model, retention assessment, pile strategy and production test.

    View Published Magnetic-Handling Solution →

    published electromagnetic handling crane engineering reference by Henan Mine Crane
    Published references are evaluated for transferable engineering functions while application-specific claims remain limited to the stated project record.

    Metal Recycling Crane Price and Budget Scope

    A complete metal recycling crane has no reliable catalog price because crane capacity, duty, span, attachment, control level, runway or gantry scope, site environment, installation and acceptance obligations change the engineered package. Public prices reviewed on 21 September 2026 are shown only to distinguish equipment levels; they are not equivalent quotations or a Henan Mine Crane project offer.

    Public Market Reference Published Price Supply Level Interpretation
    Excavator Hydraulic Grapple Listing US$150–1,000 per piece Low-cost excavator attachment listing Not a crane-mounted industrial scrap grab and not comparable with an engineered recycling crane
    30 t SWL Electro-Hydraulic Steel Scrap Grab Listing US$8,000–24,000 per piece Purpose-built attachment price signal Grab only; crane, rotator interface, cable system, controls, freight, commissioning and compliance scope require confirmation
    Customized Electric-Hydraulic Orange-Peel Grab Listing US$20,000–30,000 per piece Industrial grab marketplace reference Attachment-only figure without a normalized scrap mix, volume, deadweight, wear package or project documentation
    Four-Rope Orange-Peel Scrap Grab Listing US$10,000–200,000 per piece Very broad marketplace range Range reflects widely different sizes and specifications and cannot establish a crane project budget
    Complete Engineered Metal Recycling Crane Project Project-specific RFQ Crane, selected attachment, controls and contracted services A defensible total requires an approved duty, representative scrap data, site interfaces, destination and commercial boundary

    Primary Price Drivers

    Gross capacity and net payload; span and lift; duty classification and speeds; magnet or grab type and size; rotation; gantry or runway; outdoor and corrosion package; cabin; automation; safety zoning; plant interfaces; local code, documentation and certification.

    Commercial Scope to Reconcile

    Runway rails and structural work; gantry foundations; electrification; freight and insurance; duties and taxes; erection equipment; mechanical and electrical installation; supervision; commissioning; test loads or scrap; training; spares, warranty and production acceptance.

    Price interpretation: an excavator grapple, a crane-mounted scrap grab and an installed recycling-crane system represent different equipment and risk levels. Comparable proposals must use the same load data, duty, standards, exclusions, Incoterm, destination and acceptance criteria.

    Engineering and Procurement Deliverables

    A procurement-ready proposal defines measurable performance, interfaces, evidence and commercial boundaries.

    Technical Proposal

    Design basis, crane arrangement, capacities, duty class, speeds, attachment concept, expected pickup assumptions, environmental protection, control level and deviations.

    Interface Schedule

    Wheel reactions, power, grounding, communications, process I/O, operating zones, foundation or runway boundary, erection needs and third-party responsibilities.

    Attachment Data

    Deadweight, dimensions, volume or magnetic characteristics, service connections, rated limits, wear parts, inspection method, proof test and representative-material test plan.

    Safety Documentation

    Risk-assessment inputs, safety-function list, exclusion zones, attachment logic, power-loss behavior, isolation, emergency states and required conformity records.

    Quality and O&M Records

    Inspection and test plan, material and welding records as specified, coating reports, component certificates, manuals, lubrication plan, training and recommended spares.

    Commercial Schedule

    Price, Incoterm, milestones, packing, freight boundary, installation, commissioning, training, acceptance, warranty, exclusions, validity and optional lifecycle services.

    Metal Recycling Crane RFQ Information

    The following data supports a configuration-based technical and commercial proposal.

    Scrap and Attachment Data

    Ferrous and nonferrous percentage; material families; piece size, maximum single piece, loose density, temperature and contaminants; photographs or samples; preferred magnet, orange-peel grab, bale device or hook.

    Process and Duty Data

    Receiving, pile, shear, shredder, baler, hopper and dispatch routes; tonnes per hour; average pickup; lifts per hour; shifts; annual hours; load spectrum; travel paths and availability target.

    Site and Environment Data

    Indoor or outdoor location; span, lift and runway length; drawings; wheel-load limits; pile and vehicle envelopes; temperature, wind, dust, corrosion and fire conditions; power supply and project destination.

    Controls and Commercial Data

    Cabin, radio, assisted or automatic mode; cameras and weighing; process PLC or WMS interface; safety zones; governing standard; Incoterm; freight, installation, commissioning and testing boundary.

    Frequently Asked Questions

    Which crane is suitable for a scrap yard?

    A double-girder overhead crane suits a covered bay with an adequate runway. A gantry crane suits an open yard. The attachment is then selected from scrap composition: magnet for validated ferrous material, orange-peel grab for mixed or irregular scrap, and hook-based devices for defined loads.

    Can one crane handle ferrous and nonferrous scrap?

    Yes, when a suitable mechanical grab is used or a controlled attachment-change system is provided. An electromagnet alone cannot lift nonferrous material. Changeover time, attachment parking and retained payload must be included in the operating plan.

    How is metal recycling crane capacity determined?

    Rated capacity starts with the maximum gross suspended load. Net scrap payload equals the available rating after the attachment, hook block, rotator, beam and service equipment are included. Duty, dynamic effects and governing code are then applied.

    Does magnet capacity equal loose-scrap lifting capacity?

    No. Loose-scrap pickup depends on material, contact, air gaps, piece geometry, pile depth and temperature. Catalog test-plate values require application-specific derating and representative production trials.

    What grab is used for irregular scrap?

    A multi-tine orange-peel grab is commonly selected. Open, semi-closed or closed tine geometry is matched to bulky scrap, mixed or sheared scrap, or smaller pieces and chips. Volume, deadweight, penetration, closure force and wear remain project-specific.

    Can a recycling crane feed a shredder or baler automatically?

    Yes. Automatic or assisted feeding can use position tracking, pile profiling, level signals and process permissives. Destination availability, safe release, collision control and manual recovery require a documented interface specification.

    How much does a metal recycling crane cost?

    Attachment listings can range from a few thousand dollars to much higher values, but they do not establish the installed crane cost. A project price requires capacity, span, duty, attachment, throughput, environment, runway or gantry, controls, destination and supply boundary.

    Can an existing runway be reused?

    Only after geometry, rail alignment, condition, fatigue history, beams, columns, connections and foundations are verified against the proposed vertical, lateral, longitudinal and buffer reactions.

    Request a Metal Recycling Crane Quote

    Submit the scrap families, photographs or sample data, maximum piece and bulk density, required throughput, preferred attachment, span, lift, runway or yard drawings, duty schedule, operating environment, control level, process interfaces, power supply, destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.
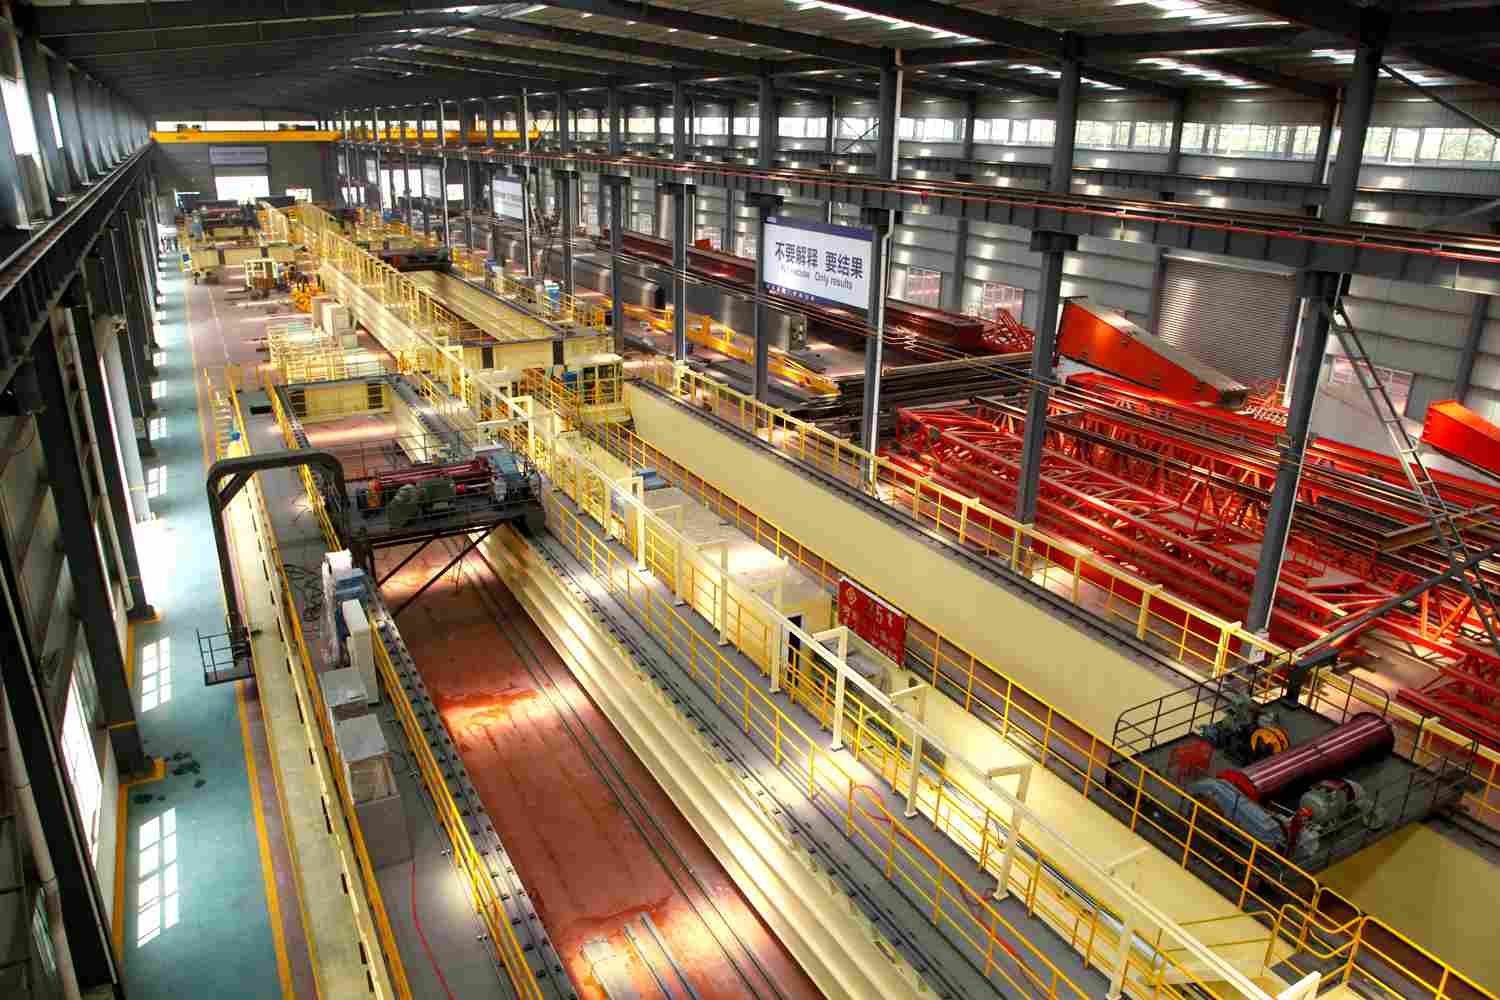
    Henan Mine CraneDiscuss your requirements ↗
  • Ladle Handling Crane

    Ladle Handling Crane

    Ladle Handling Crane

    Henan Mine Crane · Engineered Molten-Metal Handling Systems

    Ladle Handling Crane

    Heavy-duty metallurgical bridge cranes engineered for lifting, transporting and controlled pouring of molten-metal ladles in steelmaking, foundry and non-ferrous smelting plants.

    Henan Mine Crane configures each ladle crane around the maximum suspended mass, ladle geometry, transfer route, pouring method, furnace and casting-machine interfaces, thermal exposure, operating cycle, runway capacity and destination compliance requirements.

    four girder ladle handling crane for molten metal transfer
    A ladle handling crane requires a process-specific load path, thermal protection, control philosophy and safety architecture for molten-metal service.

    PROCESS AREAS

    Converter, EAF, Refining, Casting & Smelting

    CRANE CONFIGURATIONS

    Double Girder or Four Girder, Main & Auxiliary Trolley

    OPERATING DUTY

    Project-Specific Metallurgical Duty, A7–A8 Available

    PRICE BASIS

    Engineered Project Quotation

    What Is a Ladle Handling Crane?

    A ladle handling crane is a metallurgical overhead crane designed to lift a full ladle, move it between ironmaking, steelmaking, refining and casting stations, and support controlled pouring when the process requires it. It is also described as a ladle crane, casting crane, foundry crane or molten-metal handling crane. Unlike a general-purpose bridge crane, the machine is part of the steelmaking process and must remain controllable under heavy cyclic loading, radiant heat, dust and the consequences of a suspended molten-metal load.

    The main lifting device commonly uses a gantry-type ladle beam with two plate hooks engaging the ladle trunnions. This arrangement distributes the load through two lifting points and stabilizes the vessel during transfer. A separate auxiliary hook may be used to tilt the ladle for pouring, handle covers or support maintenance duties. The precise hook arrangement, trolley layout and permitted operating combinations are defined from the ladle design and process route.

    Crane capacity is based on the maximum gross suspended load—not only the mass of liquid metal. The calculation includes the full ladle shell and refractory lining, molten metal, residual slag, gantry lifting attachment, plate hooks, ropes, blocks and any process tooling carried below the trolley. The purchaser must also define ladle dimensions, trunnion spacing, center of gravity, filling level, pickup elevations and the maximum permissible tilt.

    Ladle Handling Crane Types

    01 · Double-Girder Ladle Crane

    A heavy-duty bridge with a metallurgical trolley and gantry-type ladle attachment for direct molten-metal transfer. Henan Mine Crane offers double-girder casting-crane configurations in the 50–150 t range, with project-specific capacity, span, lift and A7–A8 duty selection.

    02 · Four-Girder Ladle Crane

    A four-girder, four- or six-rail structure with separate main and auxiliary trolleys for ultra-heavy ladles, frequent production cycles and controlled pouring. Available Henan Mine Crane configurations extend from 200/50 t to 500/200 t, subject to final engineering.

    03 · Main-and-Auxiliary Trolley Crane

    The main trolley lifts and transports the full ladle through the gantry beam and plate hooks. The auxiliary trolley provides a separate hook for tilting, pouring, ladle-cover handling or maintenance. Controls restrict unsafe combinations and define coordinated motion.

    04 · Metallurgical Bridge Crane

    A project-configured metallurgical crane for molten metal, hot components or furnace-area materials. The exact lifting device, braking architecture and protection level determine whether it is suitable for direct ladle service; the product name alone is not sufficient.

    05 · Automated Ladle Transfer Crane

    Position feedback, variable-frequency drives, anti-sway functions, route permissions and process handshakes support repeatable transfers between furnace, refining and casting stations. Automation scope is defined with the plant control and safety systems.

    06 · Auxiliary and Maintenance Crane

    A separate crane can handle ladle covers, refractory equipment, furnace components and maintenance loads. Unless it is specifically engineered and accepted for molten-metal service, it must not be treated as a substitute for the production ladle crane.

    Compare Ladle Handling Crane Configurations

    The correct crane structure follows gross suspended mass, process duty, ladle geometry, pouring method, availability requirement and runway limitations. Two cranes with the same nominal capacity can have substantially different load paths, redundancy, trolley arrangements and lifecycle performance.

    Configuration Typical Application Lifting Arrangement Principal Selection Basis Important Limitation
    Double-Girder Ladle Crane Medium- to heavy-capacity ladle transfer and pouring Single metallurgical trolley or main/auxiliary hoist arrangement Gross load, cycle histogram, span, heat exposure, hook approach and runway reactions Not automatically suitable for ultra-heavy or high-availability duties without full risk review
    Four-Girder Ladle Crane Ultra-heavy ladles, intensive steelmaking and critical production bays Independent main and auxiliary trolleys on dedicated rails Main/auxiliary capacities, rail layout, structural stiffness, maintainability and fault tolerance Higher self-weight, wheel loads, building demand and capital scope
    Automated Ladle Transfer Crane Repeatable furnace-to-refining-to-casting routes Process trolley with feedback, zoning and plant handshakes Positioning, route logic, safe states, redundancy, recovery and system integration Requires a defined control boundary and validated manual recovery mode
    General Metallurgical Crane Hot materials, furnace components and auxiliary production handling Forged hook, beam or process attachment selected for the load Temperature, dust, duty, load type and operating method Cannot be assumed suitable for a suspended full ladle
    Maintenance or Service Crane Ladle covers, refractory equipment and shutdown maintenance General hook or maintenance attachment Maximum component mass, outage plan, access and infrequent duty Must not carry molten metal unless designed and accepted for that service

    Selection principle: a general bridge crane does not become a ladle crane by adding heat shields. Molten-metal service requires a coordinated structural, mechanical, electrical, control, inspection and emergency-response design.

    Match the Ladle Crane to the Metallurgical Process Area

    The handling route should be mapped from pickup to set-down before the bridge, trolley and hoist arrangement is selected. Furnace structures, fume-extraction ducts, ladle cars, transfer aisles, refining stations, casting-machine turrets, emergency set-down positions and maintenance access can all control the crane envelope.

    Each station requires verified coordinates, approach clearances and permitted motions. A workable general arrangement also considers where a loaded crane may wait, how another crane passes or shares a bay, and where a full ladle can be safely placed after a drive, brake, power or process interruption.

    Production and maintenance duties should be separated where heat exposure, working envelope, attachment requirements or availability targets make one shared crane unsuitable. This avoids using the primary ladle crane for tasks that interfere with the steelmaking sequence.

    double girder ladle crane in a steelmaking workshop
    The crane configuration must follow the ladle route, furnace interfaces, casting stations and required production availability.
    Process Area Primary Lift Crane Function Critical Interfaces Design Emphasis
    Blast-furnace or hot-metal bay Full hot-metal ladle or transfer vessel Pickup, transport and controlled placement Tapping area, ladle car, transfer aisle and downstream steelmaking bay Heat exposure, route clearance, stable transfer and emergency set-down
    Converter or electric-arc-furnace bay Steel ladle, hot-metal ladle or charging vessel Furnace approach, pickup, transfer and controlled process positioning Furnace shell, hood, ducts, platforms, charging route and exclusion zones Heavy duty, radiant heat, precise approach and availability
    Secondary refining station Full steel ladle Transfer to and from LF, RH, VD or treatment station Electrode or vacuum equipment, covers, platforms and ladle car Accurate positioning, process interlocks and restricted motion zones
    Continuous-casting bay Full steel ladle Delivery to turret or casting position and removal of empty ladle Turret coordinates, casting platform, tundish route and emergency bay Repeatability, anti-sway, queue management and safe recovery
    Foundry pouring aisle Foundry ladle and controlled pour Transport from furnace and tilt above molds or pouring stations Mold line, pouring platform, aisle access and auxiliary-hook geometry Low-speed control, visibility, tilt management and splash exposure
    Non-ferrous smelting and casting Molten aluminum, copper or alloy ladle Transfer and controlled placement or pouring Furnace, holding station, casting machine and ventilation system Material-specific heat, corrosion, fumes and attachment design

    Technical Selection and Specification Framework

    A procurement specification should define the production duty and acceptance criteria before requesting a price. Values shown below are engineering inputs, not a universal standard configuration. Final selections depend on the governing standard, plant risk assessment and approved crane duty.

    Specification Item Information to Provide Engineering Decision Why It Changes the Crane
    Rated capacity Full ladle, molten metal, slag, lining, beam, plate hooks, blocks and tooling Main and auxiliary capacities, overload basis and load combinations Controls hoist, ropes, drums, trolley, bridge, wheels and runway reactions
    Ladle and trunnion data Overall dimensions, trunnion diameter/spacing, center of gravity and allowable tilt Gantry beam, plate-hook profile, headroom, reeving and pickup geometry Determines secure engagement, clearance and load stability
    Span and runway Rail span, runway length/elevation, rail section and allowable wheel loads Girder form, end carriage, wheel quantity, rail gauge and structural reactions Directly affects self-weight, stiffness, building demand and price
    Lift and approaches Lowest pickup, highest hook/beam elevation, end approaches and obstructions Hoisting range, drum capacity, rope arrangement and limiting dimensions Ensures every ladle station can be reached without interference
    Duty and cycle histogram Lifts per hour, load spectrum, travel distances, shifts, annual hours and availability Mechanism classification, motor/brake thermal rating and structural fatigue basis A production ladle crane is selected by repeated duty, not capacity alone
    Speeds and control Production transfer speed, creep speed, positioning tolerance and acceleration limits Motor power, VFD control, feedback, anti-sway and braking performance Balances cycle time with stable, accurate molten-metal handling
    Environment Ambient and radiant temperature, dust, fumes, splash exposure and altitude Heat shielding, component location, cooling, enclosure and cable specification Protects mechanisms and electrical equipment in the verified zone
    Compliance and acceptance Destination, applicable standards, inspection authority and witness plan Design code matrix, documentation, tests and certification boundary Prevents late redesign and supports statutory commissioning

    Molten-Metal Safety, Controls and Protection

    Main-Hoist Braking Architecture

    Service and emergency braking functions are selected from the governing standard and project risk review. Brake torque, application sequence, monitoring and safe response to drive or power failure are documented and tested.

    Independent Limits and Overspeed Protection

    Operating limits, final limits, overspeed detection, drum and rope supervision, load monitoring and permissive logic prevent unintended overtravel. Critical channels are arranged to avoid a single undetected failure.

    Verified Load Path and Ladle Engagement

    The gantry beam, plate hooks, trunnion interface, sheaves, ropes, equalization and trolley frame are engineered as one load path. Hook engagement, wear limits and inspection access are included in operating procedures.

    Thermal and Splash Protection

    Heat shields, protected equipment locations, suitable insulation systems, heat-resistant cables, ventilation or cooling and guarded walkways are selected from measured radiant and ambient conditions.

    Controlled Motion and Collision Management

    Variable-frequency drives, creep speeds, acceleration control, position feedback, anti-sway functions, inter-crane spacing and restricted zones support stable travel through congested production bays.

    Emergency Set-Down and Recovery

    Approved set-down positions, backup or emergency functions, manual recovery boundaries, communications and rescue access are agreed with plant operations. The response must protect personnel, the ladle and downstream production equipment.

    metallurgical overhead crane for molten metal ladle transfer
    Main and auxiliary lifting functions are coordinated around ladle pickup, transport, positioning and pouring requirements.

    Ladle Transfer, Tilting and Controlled Pouring

    During transfer, the main trolley carries the loaded ladle through the gantry beam and paired plate hooks. Bridge and trolley motions use controlled acceleration and deceleration to limit load swing and molten-metal movement. Slow approach speeds are available at furnace, refining and casting positions where clearances are restricted.

    For pouring, the main hoist supports the ladle while the auxiliary hook engages the designated tilting point. The control philosophy defines which motions are permitted, the maximum allowable tilt, communication between operator positions and the conditions that stop or inhibit a pour. Independent movement remains available only within the approved operating envelope.

    Automation may include station coordinates, travel zoning, positioning feedback, anti-sway control, electronic weighing, condition monitoring and handshakes with ladle cars, furnace systems or casting equipment. Every automatic sequence requires a validated safe state and a practical recovery method for interrupted transfers.

    Documented Metallurgical Project

    Ladle Handling Cranes for a 3.2-Million-Ton Special Steel Base

    Henan Mine Crane supplied more than 30 core lifting units in one project shipment for Baowu Maanshan Iron & Steel’s 3.2-million-ton premium special-steel base. The equipment package supported steelmaking, refining and rolling operations rather than treating each crane as an isolated machine.

    The documented equipment included 200 t foundry cranes, 200/50 t four-girder foundry cranes, 160/63 t cranes, 40+40 t cranes and rotating electromagnetic-beam cranes. The 200 t and 200/50 t casting cranes were configured for ladle handling and refining duties, while the other crane types covered material transfer across the wider production route.

    For a new steelmaking project, this multi-crane approach is important: ladle transfer, refining, slab handling, maintenance and finished-steel logistics have different attachments, cycles, temperatures and safety requirements. Equipment responsibilities, shared runway zones and production recovery plans should therefore be engineered as one plant handling system.

    View the special steel base project →

    foundry crane project for a premium special steel production base
    Multi-model crane package covering ladle handling, refining support and material transfer at a premium special-steel production base.

    Engineering Deliverables and Quality Records

    A procurement-ready proposal defines the design basis, safety functions, plant interfaces, verification plan and site responsibilities. Traceable documents support technical review, manufacturing control, factory acceptance and statutory commissioning.

    Design Basis Package

    Approved load schedule, ladle and trunnion drawings, cycle histogram, general arrangement, clearance study, duty calculations, wheel loads, runway reactions, heat zones and compliance matrix.

    Safety and Control Documents

    Functional description, operating modes, brake philosophy, limit and interlock matrix, PLC and network architecture, safe states, emergency set-down logic, alarm list and recovery procedures.

    Manufacturing Quality Records

    Material traceability, welding procedures, welder qualifications, dimensional inspection, NDT, heat treatment or stress relief records, machining checks, assembly records and coating reports as contracted.

    Factory and Site Acceptance

    No-load and functional tests, brake and limit verification, overload functions, trolley and bridge motion, communications, fault simulation, proof-load plan, site commissioning and operator-maintenance training.

    Review Henan Mine Crane manufacturing and quality capabilities →

    Installation, Commissioning and Lifecycle Planning

    Runway and Site Readiness

    Survey rail span, elevation, alignment and runway capacity; confirm building clearances, erection route, crane access, furnace and casting coordinates, electrification, control networks and shutdown windows.

    Installation and Assembly

    Bridge girders, end carriages, trolley, reeving, gantry beam, plate hooks, heat shields, electrification and control cabinets are assembled under approved lifting, alignment and torque procedures.

    Commissioning and Process Trials

    Testing progresses from no-load motion and safety functions to proof-load testing, brake verification, positioning, main/auxiliary operation, interlocks, communications, dry-route simulation and controlled production trials.

    Inspection and Maintenance Strategy

    Inspection intervals follow duty, environment, regulation and manufacturer instructions. The program covers ropes, drums, sheaves, brakes, hooks, ladle beam, trunnion interface, structures, wheels, heat shields, cables, sensors and controls.

    Ladle Handling Crane Price and Supply Scope

    Ladle crane prices are project-specific because a commercially complete system may include the bridge and trolley, metallurgical lifting attachment, redundant safety functions, thermal protection, runway electrification, controls, documentation, shipping, installation and process commissioning. Capacity alone is not a reliable price basis.

    Quotation Level Typical Included Scope Principal Cost Drivers
    Double-Girder Ladle Crane Bridge, metallurgical trolley, ladle beam or gantry attachment, controls and defined safety package Gross capacity, span, lift, duty, heat zone, brake architecture and runway reactions
    Four-Girder Ladle Crane Four-girder multi-rail bridge, main and auxiliary trolleys, heavy-duty hoists, service access and monitoring Main/auxiliary ratings, wheel quantity, steel weight, machining, redundancy and erection method
    Automated Transfer System Positioning, anti-sway, zoning, plant handshakes, condition monitoring, process sequences and communications Station count, accuracy, signal boundary, software validation, redundancy and trial scope
    Turnkey Installed Project Engineering, runway interface, electrification, packing, freight, erection, commissioning, load test, training and spares Destination, trade term, local labor, access, shutdown schedule, statutory inspection and site services

    Public equipment advertisements frequently exclude the ladle attachment, process controls, runway, delivery, installation and statutory acceptance. A valid commercial comparison requires the same approved data sheet, safety-function schedule, documentation list, delivery term and site-service boundary.

    Crane Equipment

    Bridge, trolley, hoists, ropes, drums, brakes, wheels, platforms, access and electrification.

    Ladle Handling System

    Gantry beam, plate hooks, auxiliary hook, engagement geometry and inspection provisions.

    Safety and Controls

    Brake system, limits, monitoring, VFDs, PLC, positioning, zoning and process interfaces.

    Project Services

    Engineering, FAT, packing, freight, installation, commissioning, proof testing, trials and training.

    Information Required for a Ladle Handling Crane Quote

    A complete inquiry allows the crane structure, ladle interface, safety functions, plant integration and commercial boundary to be evaluated together. Preliminary drawings can be used during concept design when assumptions and unresolved values are clearly identified.

    01 · Process and crane duty

    Steelmaking, ironmaking, refining, continuous casting, foundry or non-ferrous service; production route, throughput, shifts, annual hours and required availability.

    02 · Gross suspended loads

    Maximum molten-metal charge, ladle shell and lining, slag, lifting beam, plate hooks, blocks, rigging and all abnormal but permitted load cases.

    03 · Ladle and trunnion drawings

    Ladle diameter and height, trunnion size and spacing, center of gravity, filling level, tilt point, cover, pickup tolerance and interface restrictions.

    04 · Building and runway

    Plan, sections, rail span, runway length/elevation, rail type, end approaches, headroom, building reserve, allowable wheel loads and access.

    05 · Stations and transfer route

    Furnace, ladle car, refining, casting, set-down and maintenance coordinates; ducts, platforms, obstacles, shared crane zones and exclusion areas.

    06 · Motion and performance

    Main and auxiliary speeds, creep speed, travel speeds, positioning tolerance, maximum acceleration, cycle times, load-sway limits and pour sequence.

    07 · Thermal and environmental data

    Ambient and radiant temperatures by zone, exposure duration, dust, fumes, molten splash, corrosion, altitude, indoor ventilation and operator environment.

    08 · Controls and plant interfaces

    Cabin, radio or remote station; manual, assisted or automatic modes; PLC, network protocol, ladle car, furnace, refining and casting handshakes.

    09 · Standards and acceptance

    Destination, governing crane/electrical standards, inspection authority, document language, witness points, FAT, proof-load test and process trials.

    10 · Commercial and site scope

    Delivery location and trade term, packing, freight, runway/electrification boundary, erection, commissioning, local labor, training, spares and schedule.

    Ladle Handling Crane FAQ

    How is ladle crane capacity calculated?

    Use the maximum combined mass of the filled ladle, refractory lining, molten metal, slag, gantry beam, plate hooks, blocks and all suspended tooling. Apply the design and regulatory factors required by the governing engineering basis.

    When is a four-girder ladle crane required?

    Four-girder multi-rail designs are considered for ultra-heavy capacities, intensive duty, separate main and auxiliary trolleys, high structural stiffness and critical availability. Runway capacity, maintenance access and lifecycle cost must also support the choice.

    Can a standard double-girder overhead crane carry a steel ladle?

    Not by default. Direct molten-metal service requires a suitable load path, ladle attachment, braking and limit architecture, thermal protection, operating duty, controls, inspection plan and acceptance procedure.

    What is the function of the auxiliary hook?

    The auxiliary hook may tilt the ladle for pouring, handle covers or support maintenance. Its capacity, position, reeving and permissible simultaneous operation with the main hoist are defined from the process and ladle geometry.

    Is A7 or A8 duty always necessary?

    The required duty follows the actual cycle and load spectrum. Henan Mine Crane offers A7–A8 casting-crane configurations, but final classification must be calculated from lifts per hour, operating hours, load distribution and production criticality.

    What safety functions are required for molten-metal handling?

    The final set depends on the governing standard and risk assessment. Typical subjects include braking, independent limits, overload and overspeed monitoring, emergency response, secure ladle engagement, heat protection, collision control and safe set-down.

    Can ladle transfer be automated?

    Yes. Position feedback, VFD motion, anti-sway, route zoning and plant handshakes can support assisted or automatic transfer. Safe states, manual recovery, communications and process ownership must be agreed before software development.

    What determines ladle handling crane price?

    Gross load, span, lift, duty, bridge and trolley structure, ladle attachment, brake and safety architecture, thermal protection, controls, runway interface, documentation, shipping and site services are the main cost drivers.

    Can an existing crane or runway be reused?

    Reuse is possible only after structural, mechanical, electrical and fatigue assessment. The review must confirm runway reactions, rail condition, clearances, load path, duty, heat exposure, compliance and the practical modernization boundary.

    What should be demonstrated before acceptance?

    Verify documentation, safety functions, brakes, limits, load performance, main and auxiliary motion, position control, plant interlocks, alarms, emergency response, proof testing, dry process routes, operator training and agreed production trials.

    Request a Ladle Handling Crane Proposal

    Submit the ladle and trunnion drawings, maximum gross suspended load, process route, crane span, lifting height, cycle data, thermal conditions, control interfaces, destination standards and delivery location. Henan Mine Crane will prepare a project-specific technical and commercial proposal.

    Henan Mine CraneDiscuss your requirements ↗
  • Indoor Crane Systems

    Indoor Crane Systems

    Indoor Crane Systems

    Henan Mine Crane · Engineered Indoor Material Handling Systems

    Indoor Crane Systems

    Overhead, underhung, freestanding, monorail, jib and compact gantry configurations for factories, workshops, warehouses, assembly areas and maintenance facilities.

    Henan Mine Crane develops indoor crane systems around gross suspended load, hook coverage, building structure, headroom, operating duty and material flow. Each proposal defines the crane, hoist, runway interface, controls, safety functions, electrical boundary, documentation, delivery and requested site services.

    indoor single girder overhead crane in an industrial workshop
    A top-running electric-hoist bridge crane provides full-bay indoor coverage while preserving production floor space.

    PRIMARY SYSTEM

    Overhead Bridge Crane

    SUPPORT OPTIONS

    Building or Freestanding

    COVERAGE OPTIONS

    Bay, Line or Workstation

    CONTROL OPTIONS

    Pendant, Radio, Cabin & PLC

    What Is an Indoor Crane?

    An indoor crane is a lifting system configured for material movement within a building or enclosed production area. The term describes the operating location, not one fixed machine. It can refer to a top-running overhead bridge crane, an underhung crane, a freestanding bridge, a workstation crane, a monorail, a jib crane or a compact gantry.

    The correct system begins with the required coverage. A bridge crane moves a load vertically, across the bridge and along the runway, providing three-axis coverage over a rectangular bay. A monorail follows one defined route. A jib rotates around a column or wall bracket. A workstation crane serves a smaller ergonomic handling zone. A portable gantry provides movable local lifting where permanent runway construction is not justified.

    Indoor operation removes external wind and weather requirements but does not make the project structurally simple. Roof height, runway elevation, building columns, bracing, sprinklers, ducts, lights, machines, aisles and maintenance access define the usable crane envelope. Existing steelwork must be verified for crane wheel loads, lateral forces, fatigue and connection reactions before it is assigned as a runway support.

    Henan Mine Crane supplies general industrial and process-specific indoor systems. Standard electric-hoist cranes serve workshops, warehouses and maintenance bays, while double-girder, automated, explosion-proof, cleanroom, magnetic, grab and metallurgical cranes address higher duty or controlled processes.

    Indoor Crane Types and Coverage

    Top-Running Overhead Crane

    Bridge wheels travel on rails above runway beams. Single- and double-girder arrangements provide full-bay coverage for manufacturing, fabrication, assembly, warehousing and maintenance.

    Underhung Overhead Crane

    Bridge end carriages travel beneath compatible runway beams. This arrangement can improve side approach and preserve floor area, but the suspended support structure requires engineering verification.

    Freestanding Bridge Crane

    Independent columns and runways transfer crane reactions into dedicated foundations. It is used where the existing building cannot accept crane loads or where a self-contained system is preferred.

    Workstation Crane

    Light enclosed-track or profile systems provide low rolling resistance and precise movement over a defined work cell. They are suited to repetitive ergonomic handling rather than heavy production loads.

    Monorail and Jib Crane

    A monorail follows a fixed linear or curved route, while a jib serves a circular or sector-shaped area. Both suit localized transfer, machine loading and maintenance tasks.

    Indoor Gantry Crane

    A portable or rail-mounted gantry stands on floor-running legs. It can serve leased buildings, maintenance areas or production zones without relying on elevated runway beams.

    Coverage shape should match the material route. Full rectangular coverage does not justify an overhead bridge when every load follows one fixed line, while a local jib cannot replace a bridge crane when loads move between multiple machines or production stations.

    Components and Operating Principle

    A powered indoor bridge crane combines the load-handling mechanism, moving bridge, end carriages, electrification and controls. The hoist lifts vertically, the trolley moves across the bridge and the bridge travels along parallel runways. The structure transfers operating forces into the building or independent support system.

    A complete specification identifies every interface. The crane package does not automatically include runway beams, rails, columns, foundations, incoming plant power, installation, test weights or statutory inspection. These items are assigned before quotations are compared.

    detailed components of an indoor electric overhead crane
    Bridge girder, electric hoist, end carriages, travel drives, electrification and controls operate as one coordinated lifting system.

    Bridge Structure

    One or two girders carry the moving hoist or trolley. Capacity, span, wheel loads, deflection, fatigue and available headroom determine the bridge form.

    Hoist or Trolley

    Electric chain hoists serve lighter compact handling, wire-rope hoists cover broader industrial duties and open-winch trolleys support demanding process applications.

    End Carriages

    Wheel assemblies support the bridge and provide long travel. Wheel spacing, rail profile, drive arrangement and alignment affect travel quality and runway reactions.

    Electrification

    Conductor bars or festoon systems feed the moving bridge, while festoon cable, cable track or energy chain serves the hoist trolley.

    Controls and Protection

    Pendant, radio, cabin or PLC controls operate the motions with emergency stop, brakes, motion limits, overload protection and specified alarms or interlocks.

    Runway Interface

    Rails, beams, brackets, columns and foundations receive crane forces. Structural responsibility and allowable reactions are stated in the technical offer.

    Indoor Crane Selection Considerations

    Selection begins with the load and material route, then coordinates the equipment with the building. Capacity alone cannot establish crane type, girder size, hoist duty, hook height, runway reactions or total installed cost.

    01 · Gross Suspended Load

    Include the payload, lifting beam, slings, clamps, magnets, grabs and every component below the hook. State normal and maximum load distributions.

    02 · Required Coverage

    Map pickup and placement points, travel route, machine interference, aisles and future expansion. Match the coverage shape to a bridge, monorail, jib or workstation system.

    03 · Span, Lift and Headroom

    Provide runway rail centers, lowest pickup, highest placement, rail elevation, roof clearance, load height and rigging depth.

    04 · Working Duty

    Define lifts per hour, full-load frequency, load spectrum, shifts, travel distance and annual operating hours. These values establish mechanism and structural service requirements.

    05 · Building Structure

    Confirm whether the facility can support top-running or suspended runway reactions. Existing beams and columns require calculation, condition and alignment review.

    06 · Motion and Positioning

    State required speeds, low-speed range, acceleration, stopping, anti-sway, synchronized lifting, positioning tolerance and automation interfaces.

    07 · Indoor Environment

    Temperature, dust, humidity, corrosion, washdown, cleanroom class, hazardous-area classification and electromagnetic or thermal exposure affect equipment selection.

    08 · Project Boundary

    Assign runway, rails, columns, foundations, plant power, freight, unloading, installation, commissioning, load testing, permits and inspection.

    Indoor Crane Configurations Compared

    The most suitable indoor crane provides the required coverage and duty without transferring unnecessary cost into the building, foundations or production layout.

    Configuration Coverage Typical Application Commercial Advantage Critical Limit
    Top-running single girder Full rectangular bay General manufacturing, assembly, warehouse and maintenance handling Efficient bridge weight and broad electric-hoist selection Headroom, capacity, span, duty and runway reactions must remain practical
    Top-running double girder Full rectangular bay Higher capacity, longer span, demanding duty and process handling Improved hook height, stiffness, trolley flexibility and maintenance access Higher self-weight, wheel loads, fabrication and installation scope
    Underhung bridge crane Full or sectional bay below compatible beams Lighter industrial service and buildings designed for suspended runways Preserves floor area and can improve side approach Roof loads, beam flanges, hangers, lateral restraint and connections govern feasibility
    Freestanding bridge crane Full or sectional bay on independent columns Retrofit buildings without suitable crane-supporting steel Independent support and controlled runway geometry Columns, bracing, foundations, floor use and erection access add scope
    Workstation crane Localized rectangular work cell Repetitive ergonomic handling and assembly assistance Low rolling resistance and precise manual or powered movement Lower capacity and span; not a substitute for heavy industrial bridge systems
    Monorail or jib crane Fixed line or circular sector Machine loading, line transfer and localized maintenance Concentrates investment around a defined material route Cannot provide unrestricted rectangular bay coverage
    Indoor gantry crane Local or rail-defined floor area Maintenance, leased buildings and areas without elevated runway support Independent support and possible relocation Leg clearance, floor loading, travel lanes and stability require control

    Single girder, double girder, top running and underhung describe structural arrangements. Indoor crane describes the installation environment. A valid proposal therefore identifies both the crane architecture and the facility interface.

    Indoor Crane Technical Specification Framework

    Henan Mine Crane maintains several indoor crane product families. The ranges below support preliminary configuration and are not guaranteed combinations. Final capacity, span, lift, working class, speeds and wheel loads are confirmed on the approved technical schedule and general arrangement.

    Product Family Published Capacity Position Published Span Position Lifting Height Position Working Class Position Primary Indoor Use
    Single-girder top-running bridge 1–80 t 7.5–31.5 m 9–30 m or project-defined Project-defined general industrial duty Workshop, assembly, warehouse and maintenance bays
    Intelligent electric-hoist bridge 1–32 t 7.5–31.5 m 6–30 m A5–A6 Higher-frequency production with controlled motion and digital functions
    Underhung single-girder bridge Published sizes include 1–20 t Published family to 31.5 m; final feasibility depends on support beams 6–30 m standard positions or customized A3–A5 Buildings with verified suspended runway structure
    Double-girder electric-hoist bridge 3–32 t or customized Up to 31.5 m in the published family 3–10 m or customized A3–A6 Greater stiffness, hook height, trolley access or capacity
    Multi-support double-girder underhung 3–40 t 10–80 m 6–30 m A3–A5 Large-span buildings, warehouses and aircraft maintenance facilities
    Special-environment indoor crane Model-specific Model-specific Model-specific A3–A8 based on the process Explosion-proof, cleanroom, insulated, metallurgical, grab or magnetic service

    A capacity shown within one family does not confirm suitability at every span, lift or duty. Long spans, severe load spectra, synchronized hoists, hazardous environments and process attachments require project-specific calculations and risk controls.

    Building, Runway and Headroom Interface

    The indoor crane and its supporting structure form one load path. Crane engineering supplies maximum wheel loads, wheel spacing, crane self-weight, horizontal forces and applicable operating combinations. The responsible structural party verifies runway beams, brackets, columns, roof framing, connections and foundations.

    Runway Type

    Top-running rails sit above runway beams; underhung end carriages travel beneath compatible beams. These arrangements are not interchangeable without structural review.

    Rail Geometry

    Gauge, straightness, elevation, joints, rail section and end stops influence wheel contact, skewing, vibration and component wear.

    Wheel Loads

    Maximum and minimum reactions are assessed with the trolley or hoist in governing positions, including applicable impact, braking and lateral forces.

    Vertical Envelope

    Roof bracing, ducts, sprinklers, lights and cable trays must remain clear throughout bridge and trolley travel. Highest hook position is checked on a dimensioned drawing.

    Hook Approaches

    End and side approaches determine access to machines, racks, truck lanes and walls. Nominal span alone does not establish usable floor coverage.

    Freestanding Structure

    Independent columns avoid building loads but require foundation reactions, floor-layout control, bracing, column spacing and an erection plan.

    Existing-runway reuse requires capacity, condition, rail profile, gauge, alignment, end-stop and clearance checks. Matching the rated load of the previous crane does not prove compatibility because wheel spacing and self-weight can change.

    Controls, Safety Functions and Automation

    Control architecture follows operating visibility, travel distance, load behavior and production integration. Pendant and radio controls suit many general industrial cranes. Cabin control serves applications requiring continuous elevated visibility. PLC and automated control support repeatable positioning, material tracking and coordinated process movement.

    Variable-Frequency Motion

    VFD control provides smooth acceleration, controlled deceleration and selectable low speed. It can reduce load swing and mechanical shock when correctly tuned.

    Overload and Motion Limits

    Overload protection, upper and lower hoist limits, travel limits, buffers and end stops restrict foreseeable overtravel and overload conditions.

    Braking and Emergency Stop

    Service brakes hold and stop each powered motion within the design basis. Emergency-stop circuits remove commanded motion based on the control architecture.

    Anti-Collision and Zoning

    Multiple cranes, restricted areas and fixed obstacles can require distance monitoring, slowdown zones, stop zones and interlocked access.

    Positioning and Anti-Sway

    Encoders, laser or other position feedback, closed-loop drives and anti-sway logic support repetitive placement and controlled automated cycles.

    Inspection Access

    Platforms, walkways, access points, lighting and isolation provisions are included where required for safe inspection and maintenance of the selected configuration.

    Indoor Crane Applications

    Fabrication and Machining

    Transfers plate, profiles, fixtures, tools, machine parts and welded assemblies between cutting, welding, machining, inspection and dispatch stations.

    Assembly and Production

    Positions components and subassemblies where smooth motion, controlled low speed and accurate hook approach support cycle time and product quality.

    Warehouse and Logistics

    Moves machinery, dies, steel products, pallets and unit loads while preserving floor lanes for production, storage and vehicle traffic.

    Maintenance Facilities

    Provides controlled removal and installation of motors, pumps, gearboxes, dies, vehicle components and plant machinery.

    Heavy Manufacturing

    Double-girder and process cranes handle large weldments, transformers, turbines, construction machinery and other high-value assemblies.

    Controlled Environments

    Cleanroom, explosion-proof, dust-controlled, corrosion-resistant or insulated cranes require declared environmental classification and dedicated components.

    Molten metal, permanent magnets, high-temperature loads, explosive atmospheres, corrosive exposure and unattended automation require dedicated product selection. These duties should not be treated as optional additions to a conventional workshop crane.

    Project Experience: 300+ Intelligent Cranes for XCMG Manufacturing

    indoor intelligent crane installed for industrial manufacturing
    Indoor crane fleets can combine bridge, gantry and specialized configurations under a common project control and production-integration strategy.

    Henan Mine Crane reports the successive supply of more than 300 intelligent cranes of various types for XCMG manufacturing operations. The equipment supports assembly and structural-component movement across engineering-machinery production processes.

    A multi-bay manufacturing program can require different capacities, spans, duties and controls while preserving consistent operator interfaces, documentation, maintenance principles and spare-parts planning. High-precision positioning, digital controls, remote monitoring and production-system integration are applied to suit the process task.

    For a comparable indoor crane program, each bay requires an individual load and building assessment. A coordinated fleet specification can then standardize controls, safety functions, component preferences, inspection records and training without forcing every process into one crane model.

    View Manufacturing Project →

    Engineering, Manufacturing, Installation and Acceptance

    automated crane girder welding workstation at Henan Mine Crane
    Controlled fabrication, dimensional inspection and documented testing connect the approved indoor crane design to the installed system.

    Project control connects approved operating data to design, fabrication, inspection, packing, erection and handover. General arrangement drawings, wheel loads, electrical data and building interfaces are approved before bridge dimensions or runway connections are finalized.

    Site acceptance begins with runway or support verification, then proceeds through assembly, alignment, electrical checks, protective-device settings, no-load operation, specified load testing, training and handover documentation.

    Supply Package Typical Content Approval Control Commercial Boundary
    Crane equipment Bridge, hoist or trolley, end carriages, drives, wheels, buffers, controls and specified access items Capacity, span, lift, duty, speeds and reactions approved Shipping splits and installation hardware listed
    Runway and supports Rails, clips, beams, brackets, columns, end stops and foundations where contracted Travel length, rail section, support spacing and structural reactions approved Building and civil work expressly included or excluded
    Electrical system Panels, VFDs, pendant or radio, crane wiring, moving electrification, alarms and interlocks Voltage, control philosophy, enclosure and interface confirmed Incoming supply and runway feed responsibility assigned
    Documents and inspection Drawings, manuals, component data, electrical diagrams, inspection and test records Language, review stages, witness points and acceptance criteria agreed Final document package listed
    Logistics and erection Export packing, freight, unloading, assembly, alignment, wiring and site supervision as contracted Access, laydown area, lifting equipment, labor and permits assigned Incoterm and site-service responsibilities stated
    Testing and handover No-load checks, functional tests, load testing, commissioning, training and spare-parts schedule Test weights, instruments and inspection authority confirmed Statutory acceptance and ongoing maintenance responsibilities assigned

    Indoor Crane Price and Total Installed Cost

    Indoor crane prices vary by configuration and supply boundary. A component kit, equipment package and commissioned system are not equivalent. The values below are current public North American market positions for preliminary budgeting, not fixed Henan Mine Crane quotations.

    Configuration Indicative Market Position Published Basis Items Requiring Confirmation
    Wall- or column-mounted jib, 1–2 t Approximately US$10,000–15,000 installed Localized 10 ft class lifting area under conventional conditions Building connection, rotation, hoist, electrical work and installation access
    Freestanding jib crane Approximately US$20,000–25,000 installed Typical freestanding system before major foundation additions Foundation can add approximately US$15,000–20,000 in the cited market
    Monorail crane, 1–2 t Approximately US$15,000–25,000 Ceiling-hung or freestanding 20–25 ft class systems with hoist Track support, curves, power feed, installation and structural verification
    Workstation bridge crane Approximately US$30,000 at 1 t; US$40,000 at 2 t 20 ft × 25 ft class coverage under the stated market conditions Freestanding support can add about 30%; hoist, runway length and site work vary
    Single-girder bridge crane Approximately US$40,000 at 5 t; US$65,000 at 10 t 5 t near 40 ft span base crane; stated 10 t position includes installation Runway, conductor system, building work, access, freight and load testing
    Double-girder bridge crane Approximately US$60,000 at 5 t; close to US$100,000 at 10 t General North American project positions under conventional conditions Trolley, span, lift, duty, platforms, runway, automation and installation
    Special-process or automated indoor crane Project quotation Engineered system for the declared production process and environment Redundancy, attachment, positioning, controls, certification, runway and commissioning

    Quotation comparison: capacity, span, lift, duty, speeds, hoist, bridge steel, runway, supports, electrification, controls, documents, freight, installation and testing should be normalized before commercial evaluation.

    Market positions were checked in September 2026 for capital-planning context. Currency, region, steel cost, building condition, specification and site access can materially change contract value.

    Quote Information and Frequently Asked Questions

    A complete enquiry should provide gross suspended load, normal load spectrum, load dimensions, attachment, pickup and placement points, span, runway length, lifting height, rail elevation, roof clearance, operating cycle, speeds, control method, environment, power supply, building information, destination and required supply boundary.

    Load and Process Data

    Maximum and routine loads, attachment mass, dimensions, center of gravity, lifting points, cycles, travel route and production consequence.

    Building and Coverage Data

    Bay dimensions, span, travel length, rail elevation, hook approaches, roof obstacles, columns and existing runway details.

    Operating and Control Data

    Working shifts, load spectrum, speeds, low-speed positioning, pendant, radio, cabin, PLC, anti-sway and system integration.

    Commercial and Site Data

    Destination, voltage, Incoterm, installation resources, permits, test weights, inspection authority and requested documentation.

    Which crane type is suitable for an indoor workshop?

    A top-running single-girder electric-hoist crane is a common starting point for general workshop handling. Underhung, freestanding, double-girder, workstation, monorail or jib systems can be more suitable after coverage, structure, duty and headroom are assessed.

    What is the difference between an indoor crane and an overhead crane?

    Indoor crane describes the operating environment. Overhead crane identifies a bridge moving along elevated runways. Most industrial indoor cranes are overhead bridge systems, but indoor equipment also includes monorails, jibs, workstation cranes and gantries.

    How much does an indoor crane cost?

    Current public North American positions extend from approximately US$10,000–25,000 for selected jibs and monorails to about US$40,000 for a conventional 5 t single-girder bridge and around US$60,000 for a 5 t double-girder bridge. Scope and region govern final value.

    Can an indoor crane use the existing building structure?

    Building-supported installation is possible after runway beams, columns, roof framing, connections and foundations are verified for crane reactions, fatigue, alignment and clearances.

    When is a freestanding crane required?

    Independent columns are considered when the building cannot accept crane loads, when structural information is unavailable, or when a self-contained runway provides better project control. Foundations and floor use become part of the project.

    How is the required crane capacity calculated?

    Capacity is based on the maximum gross suspended load, including payload, lifting beam, slings, clamps, magnets, grabs and every below-hook component. Dynamic, duty and applicable design factors are then applied.

    Are runway and installation included in the quotation?

    Runway steel, rails, columns, foundations, plant power, freight, erection, test weights and local inspection are included only when expressly listed in the commercial scope.

    What documents support final acceptance?

    The handover package can include approved drawings, wheel-load data, electrical diagrams, manuals, component information, inspection results, factory test documents, commissioning settings and site load-test records.

    Request an Indoor Crane Quote

    Submit the gross load, coverage route, span, lifting height, runway length, duty, building information, power supply, controls, operating environment, destination and required supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.

    Henan Mine CraneDiscuss your requirements ↗
  • Hydropower Plant Crane

    Hydropower Plant Crane

    Hydropower Plant Crane

    Henan Mine Crane · Hydropower Lifting Systems

    Hydropower Plant Crane

    Engineered powerhouse overhead cranes and dam-site gantry cranes for turbine-generator erection, major maintenance, intake gates, stoplogs, trash racks and spillway service.

    Henan Mine Crane configures each lifting system around the approved critical load, lifting path, plant geometry, civil interface, operating environment and project acceptance requirements.

    Henan Mine Crane 600t low-headroom overhead crane for a pumped-storage hydropower plant
    A powerhouse crane must support both generating-unit erection and the station’s long-term overhaul strategy.

    Core applications
    Turbine-generator work and water-control equipment

    Primary systems
    Powerhouse bridge crane and rail-mounted gantry crane

    Engineering basis
    Critical lift, coverage, duty and civil interfaces

    Commercial model
    Project-specific technical and price proposal

    One Hydropower Project, Several Distinct Lifting Duties

    The powerhouse crane handles the station’s highest-value components. During construction it supports the approved installation sequence for turbine runners, generator rotors and stators, shafts, covers and related assemblies. After commissioning, the same crane must provide the hook coverage and controlled motion required for scheduled outages and major overhaul work.

    Dam and waterway operations require a different machine. A rail-mounted gantry crane may handle intake gates, spillway gates, stoplogs, trash racks or maintenance equipment at positions distributed along the dam crest. Its structure, lifting media, below-the-hook device, outdoor protection and rail interface are therefore designed for the gate schedule rather than for turbine-hall work.

    Installed generating output in MW does not determine crane capacity in tonnes. The crane rating comes from the heaviest verified suspended load, including the component, lifting beam, slings, shackles and other rigging, together with the specified load path and operating method.

    Hydropower Plant Crane Configurations

    01 · Powerhouse Overhead Crane

    A double-girder bridge crane for generating-unit erection, rotor and stator handling, turbine disassembly and scheduled maintenance across the powerhouse bay.

    02 · Pumped-Storage Powerhouse Crane

    A high-capacity, frequently low-headroom arrangement for underground caverns, with project-defined synchronized lifting, precision motion and monitoring functions.

    03 · Dam-Crest Gantry Crane

    A rail-mounted outdoor crane serving multiple gate or stoplog positions, engineered for long travel, wind exposure, drainage, corrosion protection and safe parking.

    04 · Intake Gate and Stoplog Crane

    A lifting system with a purpose-designed spreader or engagement device for intake gates, emergency gates, stoplogs and trash racks at specified slots.

    05 · Tailrace or Draft-Tube Service Crane

    A separate crane or hoist for downstream gates, draft-tube stoplogs and maintenance tasks where access, water level and lifting depth differ from the dam crest.

    06 · Auxiliary Maintenance Crane

    An appropriately rated bridge crane, monorail or electric-hoist system for valve, pump, workshop and service-bay loads that do not require the main crane.

    Compare Hydropower Crane and Gate-Lifting Options

    The correct machine is selected from the load, location and operating sequence. These configurations are complementary and should not be treated as interchangeable quotations.

    Lifting configuration Primary duty Critical design inputs Procurement distinction
    Double-girder powerhouse overhead crane Turbine-generator erection and overhaul Critical suspended load, hook approach, lift height, runway reactions Heavy engineered system integrated with the powerhouse
    Dam or intake gantry crane Gate, stoplog and trash-rack handling Gate weight, slot positions, lifting depth, rail layout, outdoor environment Mobile outdoor system with project-specific spreader
    Fixed gate hoist Routine operation of one dedicated gate or gate group Gate forces, travel, connection points and operating sequence Not a traveling crane and normally tied to a fixed location
    Electric-hoist maintenance crane Pumps, valves and smaller workshop loads Local load, headroom, frequency and coverage Economical for defined service loads, not a substitute for the critical lift

    Select Capacity from the Critical Lift

    For a powerhouse crane, the critical lift may be a generator rotor, stator, turbine runner, main shaft or a combined assembly defined by the turbine supplier. Rated capacity must cover the complete suspended mass, not only the equipment nameplate weight. The lifting beam, hook block, slings, shackles and temporary tooling are included in the lift calculation as applicable.

    Large circular components require verified lifting points, centre of gravity, allowable inclination and clearances through the erection bay. If two hooks, two trolleys or two cranes are involved, permissible load sharing and synchronization must be engineered. Two nameplate ratings cannot simply be added to authorize a combined lift.

    For a gate crane, the design input includes gate or stoplog dead weight together with seating, friction, water-pressure effects and the approved operating condition. The hydropower designer defines the governing forces and lifting sequence for the crane supplier.

    Critical Lift Data

    Maximum component and complete rigging weight

    Component dimensions, centre of gravity and lifting points

    Required main and auxiliary hook ratings

    Lowest pickup and highest transfer elevations

    End approach, side approach and laydown area

    Approved operating sequence and acceptance criteria

    Technical Specification for a Hydropower Plant Crane

    Final values are established from the EPC drawings, turbine or gate supplier data, structural design and operating philosophy. Henan Mine Crane can develop the general arrangement and technical proposal after the following project inputs are confirmed.

    Specification item Project information required
    Main and auxiliary capacity Heaviest complete suspended load and separately defined service loads
    Span and runway Rail gauge, runway length, rail profile, support spacing and allowable wheel reactions
    Lifting height or depth Hook travel above and below rail, gate-slot depth and required operating elevations
    Hook and spreader coverage Generating units, erection bay, gate slots, storage racks and maintenance areas
    Duty and load spectrum Construction lifts, overhaul frequency, gate cycles and expected operating life
    Speeds and positioning Normal and slow speeds, acceleration, stopping behavior and positioning tolerance
    Environment Indoor or outdoor location, humidity, condensation, temperature, corrosion, wind and seismic data
    Electrical and control system Site power, control station, communications, monitoring and plant-system interfaces
    Applicable standards Contract code, local regulations, inspection plan and required certification
    Execution scope Packing, transport limits, erection access, supervision, commissioning, load test and training

    Precision Control and Safety Architecture

    Controlled Low-Speed Motion

    Variable-frequency drives can provide smooth acceleration, reduced mechanical shock and a specified slow-speed range for alignment over the turbine pit or gate slot.

    Hook Synchronization

    Where the approved lift uses two hooks or lifting points, feedback and control functions are configured to maintain the project-defined relationship and stop on unacceptable deviation.

    Braking and Limits

    Hoisting brakes, upper and lower limits, overload protection, travel limits, buffers and emergency functions are selected to the risk assessment and applicable contract standard.

    Anti-Sway and Monitoring

    Project-defined anti-sway, position feedback, fault recording and operating-data monitoring can support repeatable heavy lifts and maintenance planning.

    Crane and Runway Interface

    Wheel loads, skew control, rail tolerances, end stops and structural deflection criteria are coordinated with the powerhouse or dam civil design.

    Maintenance Access

    Service platforms, guarded access, inspection points, lighting and maintainable component placement are incorporated according to the approved arrangement.

    Hydropower Environment and Gate-Handling Requirements

    An underground powerhouse may combine high humidity, condensation, restricted access and limited headroom. Motors, brakes, enclosures, cable systems, coatings and ventilation are selected for the documented conditions. A low-headroom bridge layout can improve usable hook elevation, but it must be checked together with maintenance access and building reactions.

    Outdoor dam cranes require the specified wind design, storm parking and anchoring arrangement, corrosion-protection system, drainage, low-temperature provisions where applicable and weather-resistant electrical equipment. Wind operating limits and out-of-service securing procedures belong in the operating documentation.

    Gate and stoplog engagement is application-specific. The spreader, latching device, guide system, sensing and lifting media must match the gate geometry and approved procedure. The crane quotation should clearly identify whether spreaders, lifting beams, storage racks and gate-position interfaces are included.

    Specify the Site Conditions

    Indoor cavern or exposed dam-crest location

    Minimum and maximum ambient temperature

    Relative humidity and condensation risk

    Corrosion category and coating requirement

    Operating and out-of-service wind data

    Seismic, altitude and local electrical requirements

    Verified Project · Pumped-Storage Power Station

    600t Low-Headroom Pumped-Storage Powerhouse Crane

    Henan Mine Crane supplied a batch of lifting equipment for a pumped-storage power station, including a 600t overhead crane as the core heavy-lifting system. The crane uses a low-headroom structural arrangement developed for the restricted space of an underground powerhouse.

    The equipment incorporates full variable-frequency control, high-precision synchronized operation of two hooks, intelligent anti-sway functions and digital operating-data monitoring. Factory pre-assembly and integrated adjustment were completed before shipment to reduce interface risk during site execution.

    This project demonstrates the engineering priorities of a pumped-storage crane: high-capacity lifting, controlled multi-point handling, efficient use of cavern headroom and traceable operating status. Its 600t rating is project-specific and does not establish the required capacity for another station.

    View the 600t Pumped-Storage Crane Project

    600t low-headroom double-hook overhead crane manufactured for a pumped-storage power station
    600t-class hydropower lifting equipment prepared for a pumped-storage powerhouse project.

    Engineering Documentation and Quality Control

    Hydropower lifting equipment is integrated with civil works, generating equipment and the construction schedule. The technical submission can be structured around the contract’s document register and inspection plan, with responsibilities clearly assigned before manufacturing.

    Design Package

    General arrangement, wheel loads, hook approaches, mechanism data, electrical architecture and agreed calculation documents.

    Manufacturing Control

    Material traceability, welding and inspection records, dimensional control, mechanism checks and agreed witness points.

    Testing and Handover

    Factory tests, site commissioning, protection verification, load testing, manuals, spare-parts documentation and training records.

    24+
    Years of crane manufacturing

    5,100+
    Employees

    122+
    Countries and regions served

    3,500+
    Manufacturing and testing equipment sets

    Installation, Commissioning and Lifecycle Service

    Early Civil Coordination

    Confirm runway elevation, support reactions, rails, embedded items, access openings and crane assembly sequence before the structure is closed.

    Site Execution

    Coordinate transport dimensions, underground access, erection equipment, electrical supply, installation supervision and commissioning resources.

    Long-Term Availability

    Establish inspection intervals, lubrication points, rope and brake checks, critical spares and outage support before operational handover.

    The procurement schedule should identify when the crane is required for turbine-generator erection or gate installation, not only the final plant commissioning date. Manufacturing, delivery, runway readiness and site load testing must be aligned with those milestones.

    Hydropower Plant Crane Price and Budget Boundaries

    A hydropower plant crane has no dependable universal list price. Public online figures illustrate the scope problem: generic hydropower gantry listings may show equipment-only asking prices of approximately US$10,000–US$300,000, while major turnkey dam-crane replacement programs can extend into tens of millions of US dollars when engineering, removal, civil and rail modifications, installation, testing and multi-year execution are included. These figures are not like-for-like and are not a Henan Mine Crane quotation.

    A meaningful commercial comparison requires every bidder to price the same technical boundary. Henan Mine Crane develops the quotation after the lifting duty, structure, controls and delivery responsibilities are defined.

    Commercial package Items to confirm
    Crane equipment Bridge or gantry structure, trolley, hoists, hooks, drives, controls and protection
    Below-the-hook equipment Lifting beam, gate spreader, engagement device, slings, storage stand and sensors
    Runway and civil interface Rails, power feed, embedded parts, support checks and structural modifications
    Project execution Inspection, packing, freight, erection, supervision, commissioning and load testing
    Handover and support Documentation, training, initial spares, warranty boundary and lifecycle service

    Capacity, span, lifting height, hook arrangement, precision-control functions, environmental protection, destination and Incoterm materially affect the price. Each proposal should state its currency, validity, exclusions and responsibilities for site work.

    Hydropower Plant Crane RFQ Information

    Submit the powerhouse, dam or intake drawings; equipment lift list; maximum suspended load including rigging; component or gate dimensions; span; lifting height or depth; hook approaches; runway information; duty; speed and positioning requirements; power supply; environmental data; destination; applicable standard; delivery schedule; and requested installation and testing scope.

    Send Project RequirementsA technical configuration and itemized commercial scope can then be prepared for the same design basis.

    Frequently Asked Questions

    What type of crane is used in a hydropower powerhouse?

    A double-girder overhead crane is commonly selected for turbine-generator erection and major overhaul. Capacity, hook arrangement, span, lift height and duty are established from the station’s approved lift study.

    How is hydropower plant crane capacity calculated?

    Use the governing component weight plus the complete below-the-hook equipment and rigging, then verify the handling method and load path. The plant’s MW output is not the crane’s rated lifting capacity.

    Why may a pumped-storage crane need a low-headroom design?

    Many pumped-storage units are located in underground caverns where roof elevation and installation access are constrained. A low-headroom arrangement can improve hook elevation, subject to structural and maintenance-clearance checks.

    When are synchronized double hooks required?

    They may be specified when the approved lifting method uses two lifting points on a large component. Required load sharing, permitted deviation, feedback and stopping logic must be defined by engineering.

    What does a dam gantry crane handle?

    Depending on the project, it can handle intake or spillway gates, stoplogs, trash racks and maintenance equipment at multiple positions along a rail. The spreader and lifting sequence are matched to the gate design.

    Is a gate hoist the same as a gantry crane?

    No. A fixed gate hoist normally serves a defined gate position, while a gantry crane travels along rails and can serve multiple slots or maintenance points. The correct choice follows the operating philosophy.

    What protection is needed for an outdoor hydropower crane?

    The specification may include a suitable coating system, weather-resistant electrics, drainage, wind monitoring, rail clamps or anchoring, lightning protection and low-temperature measures based on actual site conditions.

    Can an existing hydropower crane be replaced or modernized?

    A retrofit is possible after checking the existing runway, wheel loads, clearances, electrical supply, access route and outage window. The retained structure and new equipment require a documented interface assessment.

    How much does a hydropower plant crane cost?

    There is no reliable unit price without capacity, span, lift height, hook or gate-spreader arrangement, controls, environmental protection and supply boundary. An itemized quotation is required for a valid comparison.

    What information is needed for a fast quotation?

    Provide drawings, the critical lift or gate data, span, lift height or depth, runway details, duty, environment, site power, destination, required standard, schedule and installation or commissioning scope.

    Related Hydropower Crane Products and Solutions

    Henan Mine Crane double-girder overhead crane

    Double-Girder Overhead Crane

    Bridge-crane configuration for appropriately rated powerhouse and maintenance duties.

    View Details →

    Henan Mine Crane double-girder gantry crane

    Double-Girder Gantry Crane

    Heavy rail-mounted structure adaptable to engineered outdoor hydropower duties.

    View Details →

    Henan Mine Crane cross-travel overhead crane

    Cross-Travel Overhead Crane

    Track-switching access for compatible, specifically engineered maintenance routes.

    View Details →

    Henan Mine Crane double-trolley electric-hoist overhead crane

    Double-Trolley Electric-Hoist Crane

    Coordinated handling option for defined service loads and approved lifting methods.

    View Details →

    Henan Mine Crane water conservancy and hydropower lifting solution

    Hydropower Industry Solutions

    Explore lifting applications for water conservancy and hydropower projects.

    View Solutions →

    Hydropower Lifting Proposal

    Request a Hydropower Plant Crane Quote

    Share the critical lift, turbine or gate data, plant drawings, runway information, required operating environment, destination and project schedule. Henan Mine Crane will develop a defined equipment configuration and commercial scope for the hydropower facility.

    Henan Mine CraneDiscuss your requirements ↗
  • Hot Rolling Mill Crane Systems for Steel Production

    Hot Rolling Mill Crane Systems for Steel Production

    Hot Rolling Mill Crane Systems for Steel Production

    Henan Mine Crane · Hot Rolling Mill Lifting Systems

    Hot Rolling Mill Crane Systems for Steel Production

    Engineered overhead cranes for slab transfer, reheating-furnace support, roll handling, mill maintenance, plate and coil movement, finished-product storage and coordinated fleet operation.

    Henan Mine Crane configures double-girder production cranes, roll-shop cranes, slab cranes, magnetic-beam cranes, coil-handling cranes and service cranes around each process station. Capacity, duty, heat protection, attachment, speed, controls and project scope are defined by the handled load and production route.

    Henan Mine Crane hot rolling mill overhead crane in steel production workshop
    A hot-rolling facility normally uses a coordinated crane fleet rather than one universal crane configuration.

    PROCESS COVERAGE

    Slab to Finished Product

    CRANE FAMILY

    Production & Service Cranes

    ATTACHMENT OPTIONS

    Hook, Beam, Clamp & Magnet

    CONTROL OPTIONS

    Cabin, PLC & Automation

    What Is a Hot Rolling Mill Crane?

    A hot rolling mill crane is an overhead lifting system designed for the production, storage and maintenance tasks surrounding a hot-rolling line. The term covers several purpose-specific cranes because slabs, rolls, plates, coils, tooling and mechanical assemblies create different load shapes, temperatures, cycle frequencies and failure consequences.

    Production cranes may transfer hot or ambient slabs, feed process buffers, move plate or coil products and support continuous material flow. Roll-handling cranes lift work rolls, backup rolls, chocks and roll-changing equipment. Service cranes handle motors, gearboxes, mill stands, guides and other maintenance loads during planned shutdowns. A crane suitable for occasional maintenance is not automatically suitable for repeated production cycles.

    The engineering basis combines maximum gross suspended load, attachment weight, span, lifting height, hook approach, runway length, load spectrum, moves per hour, required speed, positioning tolerance and operating environment. Radiant heat, scale, dust, fumes and restricted maintenance access affect component placement, enclosures, cooling, lubrication and inspection frequency.

    A complete hot-rolling crane proposal therefore defines each crane by process station and coordinates common controls, documentation, components and spare parts across compatible units. Fleet standardization should simplify operation without forcing unlike applications into one technical specification.

    Hot Rolling Mill Crane Configurations

    01 · Slab Transfer Crane

    Moves hot or ambient slabs between continuous casting, cooling, storage and reheating-furnace preparation. Mechanical clamps, magnet beams or approved lifting beams are selected from slab temperature, geometry and stack access.

    02 · Rolling-Line Production Crane

    Supports mill-line material movement, tooling exchange and production interventions. High duty, controlled acceleration, protected electrical equipment and clear operating visibility address the heat, scale and production rhythm.

    03 · Roll-Shop and Roll-Change Crane

    Handles work rolls, backup rolls, chocks, cassettes and roll-changing equipment. Multi-point beams, auxiliary hoists, precise low-speed control and accurate hook approach support alignment and workshop safety.

    04 · Plate Handling Crane

    Uses magnets, clamps or lifting beams for plates and long products after rolling, cooling and finishing. Load flatness, plate temperature, surface quality and multi-magnet control determine the attachment system.

    05 · Coil Handling Crane

    Transfers coils with C-hooks, coil grabs, magnets or engineered beams. Coil eye orientation, width, outside diameter, mass, storage saddles and emergency lowering requirements govern configuration.

    06 · Maintenance and Service Crane

    Provides intermittent access to drives, stands, motors, gearboxes and production equipment. Useful hook approach, low-speed positioning, rigging clearance and shutdown installation access are more important than production throughput.

    Compare Hot Rolling Mill Crane Systems

    Crane System Primary Loads Typical Attachment Engineering Priority Critical Selection Data
    Slab handling crane Hot or ambient slabs and blooms Clamp, magnet beam or lifting beam High duty, thermal protection and controlled stacking Slab dimensions, temperature, cycle rate and storage layout
    Roll handling crane Work rolls, backup rolls, chocks and cassettes Roll beam, tong, hook system or dedicated attachment Precise multi-point lifting and alignment control Roll set mass, centers, pickup geometry and change sequence
    Production service crane Tooling, mill components and process loads Main and auxiliary hooks or engineered beam Frequent operation with controlled positioning Load spectrum, production interface and permitted shutdown windows
    Magnetic plate crane Ferromagnetic plates and long steel products Fixed or rotating electromagnetic beam Fast pickup with coordinated magnet groups Plate range, temperature, air gap, power-loss plan and surface protection
    Coil handling crane Hot- or cold-rolled coils within approved temperature C-hook, coil grab, magnet or fork attachment Stable coil transfer and accurate saddle placement Coil mass, eye orientation, dimensions and warehouse system
    Maintenance bridge crane Motors, gearboxes, stand components and general loads Hook block, sling and removable lifting beam Flexible access for scheduled service work Heaviest maintenance lift, headroom, approach and operating frequency

    Fleet selection rule: build the crane schedule by bay and process task, then standardize controls, component families, documentation and spare parts only where capacity, duty and environment remain compatible.

    Crane Applications Across the Hot Rolling Process

    Process Area Handling Task Crane Direction Engineering Data Control Priority
    Slab yard and buffer storage Receive, identify, stack and retrieve feed slabs Slab clamp or magnetic-beam crane Slab geometry, residual heat, stack pattern and retrieval sequence Secure pickup, anti-sway and stack-zone control
    Reheating-furnace preparation Deliver selected slabs to charging or transfer equipment Heavy-duty slab or hook-beam crane Furnace schedule, buffer capacity, temperature and transfer interface Production interlocks and controlled placement
    Roughing and finishing mill Tooling exchange, process intervention and maintenance support Double-girder production or service crane Heat, scale, obstruction, operating window and equipment access Protected electrics, precise motion and exclusion zones
    Roll shop and roll storage Move rolls, chocks, cassettes and grinding-shop loads Roll-handling crane with dedicated beam or hooks Roll dimensions, balance, pickup points and storage stands Synchronized lifting and low-speed alignment
    Cooling, cutting and plate finishing Transfer plates between cooling, leveling, cutting and inspection Magnetic, clamp or beam-equipped crane Plate temperature, flatness, length and surface requirement Attachment selection and multi-load control
    Coil or plate warehouse Stack, retrieve and dispatch finished products Coil, plate or automated warehouse crane Inventory logic, throughput, coordinates and vehicle loading Positioning, tracking, collision avoidance and recovery mode

    A rolling-mill fleet can include cranes with similar rated capacities but different mechanism classes and safety functions. Production duty, attachment mass, average load and heat exposure determine the design more reliably than capacity alone.

    Technical Selection and Specification Framework

    Henan Mine Crane has documented a 34-crane hot-rolling fleet ranging from 10 t to 100 t and also publishes specialized hot-rolling bridge-crane configurations for higher capacities. These project values demonstrate available engineering directions; final parameters are approved separately for every crane position.

    Specification Item Project Input Required Engineering Output Procurement Control
    Capacity basis Maximum load plus hook block, beam, clamp, magnet, C-hook, sling and every suspended component Net product mass and gross suspended load are stated separately Future lifts are included only when defined and structurally approved
    Span and coverage Runway rail centers, bridge travel, equipment centers and side approaches Dimensioned plan with hook or attachment coverage Building width is not substituted for crane span
    Lift and headroom Lowest pickup, highest placement, rail elevation, attachment depth and roof obstructions Dimensioned vertical section and maintenance-removal route Highest hook position and actual load height are verified together
    Duty and load spectrum Moves per hour, average load, full-load frequency, shifts, annual hours and travel distance Crane and mechanism classification for each position Production and maintenance cranes are classified independently
    Temperature and contamination Ambient air, product temperature, radiant heat, distance, scale, dust, fumes and humidity Protection schedule for structure, motors, brakes, cables, cabinets and lubrication Product surface temperature is not treated as ambient temperature
    Attachment and load control Hook, beam, clamp, magnet, C-hook, grab or roll-handling equipment Attachment drawing, mass, operating envelope and interlocks Attachment weight and geometry enter capacity and headroom calculations
    Speed and positioning Hoist, trolley, bridge, auxiliary and rotation speeds plus required low-speed range VFD, brake, encoder and anti-sway description Cycle performance is checked against stopping distance and load stability
    Controls and integration Cabin, radio, local station, PLC, cameras, automation and MES or WMS interface Control narrative, I/O schedule and fault-recovery philosophy Manual fallback and data boundary are defined before software approval
    Runway and building Rail, beam, column, foundation, power supply, access and multiple-crane arrangement Wheel loads, horizontal forces, buffer reactions and conductor data Structural and installation responsibilities are contractually assigned
    Inspection and acceptance Destination rules, document language, witness points, factory and site testing Inspection plan, test procedures and handover records Load-test weights, labor and statutory coordination are included or excluded explicitly

    Safety and Control Requirements

    Hot-rolling crane safety combines conventional overhead-crane protection with controls for hot products, long loads, production equipment, shared runways and restricted work zones. The final architecture follows the governing design basis and plant risk assessment.

    Hoisting Protection

    Overload limitation, upper and lower limits, brake monitoring, rope guidance, slack-rope protection and low-speed positioning are selected for the load and duty.

    Heat and Electrical Protection

    Heat shields, protected cabinets, temperature-rated cables, cooling or ventilation and suitable lubrication reduce radiant-heat and scale exposure.

    Long-Load and Attachment Control

    Synchronized lifting, attachment status, magnet monitoring, clamp locks and controlled release prevent skew, unequal loading and unintended load loss.

    Travel and Collision Protection

    End limits, buffers, rail sweeps, anti-collision, restricted zones and crane-separation logic address adjacent cranes and fixed production equipment.

    Operator Visibility

    Cabin position, cameras, lighting, warning devices and communication systems provide visibility around mills, stacks, vehicles and maintenance teams.

    Automation and Recovery

    Position feedback, anti-sway, permissive logic, safe stop, fault diagnosis, controlled restart and manual recovery govern automated cycles.

    Maintenance Isolation

    Accessible isolators, lockout points, platforms, walkways and component-removal zones support planned work above active production areas.

    Emergency Operating Plan

    Load retention, controlled lowering, alternate power, emergency braking and production shutdown responsibilities are documented for credible failures.

    Crane Structure, Fleet Logic and Workshop Interface

    Top-running double-girder bridges are widely applied in rolling mills because the structure supports higher capacities, open-winch trolleys, main and auxiliary hoists, service platforms and process attachments. Box-girder design, trolley arrangement and wheel distribution are selected from the span, fatigue duty, headroom and building reactions.

    Production cranes require motion profiles that combine efficient clear travel with controlled approach near the mill, stack or vehicle. Variable-frequency drives, encoders and suitable braking provide low-speed positioning without abrupt acceleration of long slabs, rolls, plates or coils. Maximum speed alone does not determine throughput; pickup, alignment and safe release often control the cycle.

    Fleet planning assigns a unique equipment number, bay, runway, load family and duty to every crane. Common operator interfaces, drive families, brakes, electrical components and documentation can reduce training and spare-parts complexity where ratings remain compatible. Process-specific attachments and protection stay unique to the workstation.

    Runway reactions, rail alignment, conductor location, maintenance platforms, mobile-crane access and removal paths should be coordinated with building and process-equipment design before fabrication. Late interface changes can affect hook coverage, wheel loads and installation cost.

    double girder hot rolling mill crane above steel production line
    Bridge structure, trolley, runway and process clearances are coordinated around the assigned production or maintenance task.

    Project Case: 34-Crane Fleet for Chongqing Panhua Plate

    Henan Mine Crane hot rolling mill bridge crane project
    A large hot-rolling project requires coordinated production, roll-handling and maintenance cranes across multiple bays.

    Henan Mine Crane supplied 34 double-girder overhead cranes for Chongqing Panhua Plate’s intelligent hot-rolling project. The documented fleet ranges from 10 t to 100 t and supports a steel-plate production base with an annual capacity of 4.5 million tonnes.

    The cranes serve production, roll handling, tooling, equipment service and maintenance positions. Capacity and duty were assigned by workstation, while compatible controls, documentation and spare-parts planning were coordinated across the fleet. This prevents a 10 t maintenance crane and a similarly rated production crane from being treated as identical equipment.

    Phased engineering, manufacturing and delivery aligned crane availability with workshop construction and commissioning. The case demonstrates the procurement value of one fleet schedule: every crane retains the required span, lift, duty, attachment and environmental protection while project-wide interfaces remain controlled.

    View Hot Rolling Crane Case →

    Engineering, Manufacturing and Quality Documentation

    A rolling-mill crane package should connect the approved process data to controlled fabrication, mechanism selection, electrical assembly, testing and handover records. Inspection requirements should be agreed before production release.

    automated double girder crane welding workstation at Henan Mine Crane
    Approved drawings, controlled welding, dimensional inspection and functional testing support traceable fleet delivery.

    Design Package

    General arrangement, wheel loads, hook approaches, mechanism class, attachment drawing, electrical demand and control narrative.

    Structural Records

    Material identification, approved welding procedures, welder qualifications, dimensions and specified non-destructive examination.

    Mechanism Data

    Motor, gearbox, brake, drum, rope, wheel, bearing, coupling and lubrication information matched to the declared duty.

    Electrical Documents

    Single-line diagram, schematics, I/O schedule, drive data, protection settings, network boundary and configured parameters.

    Inspection and Tests

    Inspection plan, witness points, dimensions, mechanisms, brakes, limits, alarms, attachment functions and contracted load testing.

    Fleet Handover

    Crane-numbered manuals, final drawings, test records, spare-parts lists, maintenance schedules and commissioning data.

    Installation, Commissioning and Lifecycle Planning

    Fleet Engineering Schedule

    List every crane by bay, quantity, capacity, span, lift, duty, attachment, power, control mode and required drawing, manufacturing and delivery date.

    Runway and Site Verification

    Confirm rail centers, elevation, alignment, support capacity, conductor arrangement, crane separation, end stops and installation access before shipment.

    Phased Packing and Delivery

    Match bridge sections, trolleys, panels, attachments and loose parts to the equipment number and destination bay. Delivery batches follow site readiness.

    Erection and Alignment

    Plan mobile-equipment access, assembly areas, lifting method, rail checks, conductor installation, attachment assembly and work near process equipment.

    Commissioning and Acceptance

    Verify brakes, limits, drives, synchronization, controls, alarms, communications and attachment functions before load and process trials.

    Operator and Maintenance Training

    Cover operating modes, warning responses, daily checks, isolation, fault recovery, attachment inspection and crane-specific limitations.

    Preventive Maintenance

    Inspection intervals reflect load cycles, heat, scale, dust and production consequence. Brakes, ropes, wheels, rails, cables and attachments receive defined wear limits.

    Fleet Spare-Parts Planning

    Standardize compatible brake, drive, contactor, encoder, sensor, limit, rope and seal families while retaining crane-specific critical spares.

    Hot Rolling Mill Crane Price and Project Cost

    Process cranes and multi-crane rolling-mill fleets require project quotations. The general bridge-crane figures below provide a current North American market baseline only; they are not fixed Henan Mine Crane prices and do not represent high-duty hot-rolling equipment.

    Budget Level Indicative Market Position Typical Scope Main Cost Drivers Commercial Control
    5 t single-girder bridge benchmark Around US$40,000 General bridge, base trolley and hoist near or below a 40 ft span Span, lift, duty, runway, electrification and installation Not a rolling-mill process-crane quotation
    10 t single-girder installed benchmark Around US$65,000 Conventional general-duty crane under stated regional conditions Building, access, controls, labor, testing and site scope Use only as a lower-level general market comparison
    5 t double-girder installed benchmark Around US$60,000 Conventional two-girder bridge under stated conditions Trolley type, headroom, span, runway and installation Does not include rolling-mill heat or process engineering
    10 t double-girder installed benchmark Around US$100,000 Conventional double-girder system under stated conditions Duty, speed, controls, runway, access and regional labor Not comparable with 50–200 t specialized process cranes
    Hot-rolling production or roll crane Project quotation Heavy-duty bridge, open-winch trolley, process attachment and environmental protection Gross load, duty, heat, attachment, speed, redundancy and documents Crane, attachment, freight and site services are separated
    Automated multi-crane fleet Project quotation Multiple cranes, controls, plant interfaces, commissioning and lifecycle package Quantity, standardization, integration, phasing, spares and acceptance Evaluate total fleet cost and production responsibility

    Commercial normalization: compare crane equipment, attachment, runway, electrification, thermal protection, automation, documentation, packing, freight, erection, commissioning, load testing, training and spare parts as separate line items.

    Information Required for a Hot Rolling Mill Crane Quote

    A complete request should contain one crane schedule covering every workshop and process position. Building drawings, equipment layouts, load sketches and project milestones should accompany the following data.

    Crane Schedule

    Quantity, equipment number, bay, capacity, span, lifting height, runway length, headroom, hook approach and required delivery sequence.

    Load and Attachment

    Load name, maximum and typical mass, dimensions, center of gravity, pickup points, temperature, attachment type and attachment mass.

    Duty and Throughput

    Moves per hour, load spectrum, shifts, annual hours, full-load frequency, travel distance, target cycle and production consequence.

    Motion and Control

    Hoist, trolley and bridge speeds, low-speed range, main and auxiliary hooks, cabin or radio control, anti-sway and positioning tolerance.

    Environment

    Ambient temperature, product temperature, radiant heat, distance, scale, dust, fumes, humidity, corrosion and electrical enclosure requirements.

    Runway and Building

    Rail section, runway beam, column spacing, rail elevation, wheel-load limits, conductor position, obstructions and installation access.

    Automation and Interfaces

    PLC or MES communication, I/O, equipment interlocks, stack or target coordinates, cameras, data records and manual recovery mode.

    Commercial and Acceptance Scope

    Trade term, packing, freight, runway, installation, load testing, third-party inspection, training, spares and schedule milestones.

    Hot Rolling Mill Crane FAQ

    Which crane types are required in a hot rolling mill?

    Typical systems include slab transfer cranes, production bridge cranes, roll-handling cranes, plate or coil cranes and maintenance cranes. The exact fleet follows process layout, load families and maintenance strategy.

    How is crane capacity selected?

    Capacity includes the maximum load and every suspended attachment. Roll beams, clamps, magnets, C-hooks, hook blocks and rigging enter the gross-load calculation. Future lifts require defined geometry and duty.

    Can one crane handle slabs, rolls and coils?

    A shared crane is possible only when capacity, attachment changes, headroom, duty, heat exposure and operating routes remain compatible. Dedicated process cranes normally provide clearer safety and throughput for frequent tasks.

    What duty class suits a rolling mill crane?

    Duty follows load spectrum, moves per hour, shifts, travel distance and operating consequence. A production crane and an intermittent maintenance crane can require different mechanism and structural classifications at the same capacity.

    How is radiant heat addressed?

    Thermal design considers product surface temperature, ambient air, exposure distance and duration. Shields, protected cabinets, suitable cables, component placement, cooling and lubrication are selected from the actual heat map.

    Can rolling mill cranes integrate with MES?

    Yes. PLC-based systems can exchange task, permissive, status, position and fault data with plant systems. Interface ownership, protocol, I/O, cybersecurity boundary and manual recovery are defined before implementation.

    What attachment is suitable for steel plate?

    Magnets support fast handling of approved ferromagnetic plates, while clamps or beams may suit restricted magnetic use or specific surface requirements. Temperature, air gap, plate range and power-loss strategy govern selection.

    How should roll changes be handled?

    A dedicated roll beam or multi-point arrangement should match roll centers, mass, balance and storage stands. Synchronized lifting, precise low-speed motion and clear exclusion zones support controlled alignment.

    Can a large crane fleet be delivered in phases?

    Yes. Drawing approval, production and shipment can follow workshop readiness. Every component and document should retain the correct crane number, bay and delivery batch throughout the project.

    What should a commercial quotation include?

    The proposal should identify crane and attachment scope, technical parameters, runway interface, heat protection, controls, documentation, testing, packing, freight, erection, commissioning, training, spares, exclusions and schedule.

    Request a Hot Rolling Mill Crane Proposal

    Submit the crane schedule, workshop layouts, load list, attachment requirements, duty, temperature conditions, runway data, power supply, controls, project milestones, destination and delivery boundary. Henan Mine Crane will prepare a coordinated technical configuration and commercial quotation.

    Henan Mine CraneDiscuss your requirements ↗
  • Heat Treatment Crane Systems

    Heat Treatment Crane Systems

    Heat Treatment Crane Systems

    Henan Mine Crane · Engineered Heat-Treatment Lifting Systems

    Heat Treatment Crane Systems

    Process cranes engineered for furnace loading and extraction, transfer of hot workpieces, controlled immersion into water, polymer, brine or oil baths, timed recovery and integration with manual or automatic heat-treatment lines.

    Henan Mine Crane configures each heat treatment crane from the maximum gross suspended load, workpiece temperature, furnace-to-bath route, required immersion time, lowering and recovery speed, bath medium, duty cycle, attachment, workshop geometry, emergency strategy and applicable project standards.

    high-speed heat treatment crane above a quenching line
    A purpose-built heat treatment crane coordinates hot-load transfer, rapid immersion, bath dwell and controlled recovery as one defined process cycle.

    PUBLISHED CAPACITY PLATFORM

    20–150 t or Custom

    PUBLISHED SPAN RANGE

    7.5–35 m

    PROCESS MOTION

    Controlled Rapid Immersion

    CONTROL OPTIONS

    Manual, PLC or Automatic

    Published ranges describe the Henan Mine Crane quenching-crane platform, not a universal model. The approved project specification governs final capacity, speed, span, lift, classification and performance.

    What Is a Heat Treatment Crane?

    A heat treatment crane is an overhead process crane designed to move workpieces, baskets, racks or fixtures between furnaces, quench tanks, wash stations, tempering equipment, cooling positions and inspection areas. The term includes general furnace-transfer cranes as well as high-speed quenching cranes that must immerse a hot load within a specified time and motion profile.

    The distinction matters. A general double-girder crane may be suitable for controlled transfer where the process has no rapid immersion requirement and the thermal, vapor, splash and duty conditions remain within its engineered limits. A quenching overhead crane requires a verified lowering speed, brake and overspeed architecture, power-loss response, load stability, bath clearance and recovery method. Substituting a general-purpose crane without this process review can compromise both treatment results and safe load control.

    Heat treatment cranes handle solid workpieces. They are not automatically suitable for ladles or molten metal. A foundry or casting crane uses a different load path and safety architecture. Henan Mine Crane develops heat-treatment systems from its quenching crane, metallurgical bridge crane and double-girder bridge crane platforms according to the actual process duty.

    Heat Treatment Crane Applications

    Vertical Shaft and Roll Quenching

    Lift long shafts, rolls or rotors in a controlled vertical orientation and lower them into a tank while maintaining clearance, stability and the specified immersion profile.

    Batch and Basket Quenching

    Transfer loaded baskets, racks or fixtures from the furnace to water, polymer, brine or oil baths with repeatable pickup, travel, immersion and drainage positions.

    Die and Mold Heat Treatment

    Handle dies, mold blocks and tool steel between heating, quenching, tempering and inspection stations with an attachment matched to geometry and hot-load behavior.

    Gear, Ring and Bearing Production

    Move rings, gears, rollers and bearing components through controlled thermal cycles where positioning, batch traceability and repeatable transfer time are required.

    Forging Heat-Treatment Bay

    Transfer heavy forgings, flanges and pressure-vessel parts from furnaces to cooling or quenching stations, including single- or dual-point handling where approved.

    Automatic Heat-Treatment Line

    Coordinate crane movements with furnace doors, tank covers, agitation systems, recipes, tracking databases and defined safe zones through an approved signal matrix.

    automatic positioning quenching overhead crane in a heat treatment workshop
    Automatic operation is defined by the complete production interface: load identification, route permissions, furnace and tank interlocks, positioning, fault handling and manual recovery.

    Components and Operating Principle

    1. Bridge and end carriages: distribute trolley, load and dynamic reactions to the runway while maintaining the required approach to furnaces and tanks.
    2. Process hoist: provides normal lifting, rapid or controlled immersion, recovery and low-speed positioning through a motion profile matched to the treatment recipe.
    3. Brakes and monitoring: use the project-defined service, holding and emergency functions, with overspeed, position, limit and load supervision where required.
    4. Below-hook equipment: may include baskets, racks, spreaders, lifting beams, tongs, clamps or vertical lifting fixtures engineered for the hot workpiece and bath.
    5. Controls and interfaces: coordinate bridge, trolley and hoist motion with furnace doors, tank equipment, restricted zones, process recipes and operator commands.
    6. Environmental protection: addresses radiant heat, steam or vapor, splash, corrosion, scale, water drainage, oil mist, cable routing, enclosure selection and maintenance access.
    quenching crane bridge and hoisting machinery for heat treatment service
    The bridge, hoist, brakes, reeving, attachment, sensors, controls and emergency functions are engineered as one process system.

    Rated-load basis: crane capacity must cover the heaviest workpiece plus the basket, rack, lifting beam, chains, fixture, hook block and every other suspended item. It must also account for retained liquid, eccentric loading, dual-point load sharing and the approved dynamic case. Workpiece mass alone is not the crane rating.

    Heat Treatment Crane Selection Considerations

    Selection begins with the treatment cycle and complete load path. Capacity, span and lift are necessary, but they do not define immersion performance, safe recovery or the interface with the furnace and tank.

    Load and Orientation

    Minimum, typical and maximum gross load; dimensions; center-of-gravity range; vertical or horizontal orientation; single or multiple pickup points; fixture mass and retained liquid.

    Transfer and Immersion Time

    Furnace-door release to bath entry, travel distance, required lowering profile, entry depth, dwell, agitation interaction, withdrawal speed and drainage time.

    Temperature and Exposure

    Workpiece temperature at pickup, furnace opening duration, radiant-heat map, steam or vapor plume, splash envelope and measured temperatures at ropes, brakes, motors, sensors and panels.

    Bath and Medium

    Tank length, width, depth and freeboard; water, polymer, brine or oil; operating temperature; agitation; covers; overflow; ventilation; fire strategy; drainage and contamination controls.

    Duty and Availability

    Lifts per hour, starts and reversals, shifts, annual hours, load spectrum, required production availability, maintenance windows and the consequence of an interrupted batch.

    Power Loss and Recovery

    Safe load state, controlled lowering or lifting, emergency power source, brake behavior, manual recovery, tank access and the permitted response at each point in the process cycle.

    Building and Runway

    Rail-center span, runway length and elevation, available headroom, hook approaches, wheel-load limits, furnace and tank obstructions, ventilation ducts and installation access.

    Controls and Acceptance

    Cabin, radio or automatic operation; positioning tolerance; anti-sway; recipe signals; traceability; safe zones; FAT, SAT and representative-load test criteria.

    Heat Treatment Crane Configurations Compared

    The correct configuration follows the process motion, load orientation and failure response. The table separates common arrangements that may look similar in a workshop layout but serve different duties.

    Configuration Typical Process Load Arrangement Defining Engineering Requirement When It Fits
    General Heat-Treatment Handling Crane Furnace charging, extraction, tempering and cooling transfer Hook, beam, basket or fixture Thermal exposure, duty, attachment and controlled low-speed positioning No rapid immersion function is required
    Vertical Quenching Crane Shaft, roll, rotor or long-part immersion Vertical fixture with guided or stabilized pickup Clearance, vertical stability, immersion speed and emergency recovery Long components must enter a deep tank vertically
    Batch or Basket Quenching Crane Grouped components or mixed production batches Basket, rack or multi-point spreader Gross batch mass, even support, retained liquid, drainage and repeatable pickup Parts are processed in a common fixture
    Automatic Quenching-Line Crane Recipe-driven furnace and tank sequence Standardized fixtures with identification Positioning, anti-sway, signal ownership, traceability and defined fallback modes Repeated routes and plant-level integration justify automation
    Heavy Forging Heat-Treatment Crane Large forgings, flanges, rings and pressure components Heavy beam, clamp, tongs or dual-point rig High gross load, eccentric cases, attachment behavior and intensive duty Heavy individual components require process-specific handling
    Foundry or Casting Crane Molten-metal ladle transfer Ladle beam and auxiliary hook Molten-metal load path and applicable foundry requirements Separate application; not a substitute for a quenching crane
    heavy-duty metallurgical bridge crane platform used for custom heat treatment crane engineering
    A custom heat-treatment configuration is selected from the actual process, not from capacity alone. Similar bridge structures can contain materially different hoist, brake, control and environmental systems.

    Preliminary Heat Treatment Crane Specifications

    These values summarize the published Henan Mine Crane quenching-crane platform and common project variables. They support an initial enquiry; they are not a substitute for the approved data sheet.

    Parameter Published Reference or Option Required Project Confirmation
    Rated Capacity 20–150 t published platform; custom engineering available Maximum gross suspended load and all abnormal load cases
    Span 7.5–35 m published range Rail-center dimension, runway condition and hook approaches
    Lifting Height 4–20 m published range Highest pickup, lowest immersion point, freeboard and hook-block geometry
    Hoisting Speed 10–30 m/min published platform reference Normal lift, creep, immersion, withdrawal and emergency motion profiles
    Working Classification A7–A8 published platform reference Applicable classification system, load spectrum, cycles and design life
    Power Supply Published options include 380 V/50 Hz and 220–660 V/60 Hz Site voltage, frequency, earthing, short-circuit data and emergency source
    Control Mode Cabin, radio, PLC-assisted or automatic Operating philosophy, visibility, safe zones, interfaces and fallback mode
    Positioning Project-specific Tolerance at furnace, tank and fixture; speed; sway; load and environmental conditions
    Environment Heat, vapor, splash and corrosion protection as required Measured component exposure, medium, ventilation and enclosure requirements
    Specification control: published product ranges can differ as the platform evolves. The signed technical agreement, general arrangement, mechanism data sheets, interface schedule and acceptance plan define the supplied crane.

    Quenching Cycle and Motion Engineering

    A useful performance specification describes the entire motion from furnace pickup to bath exit. It states when timing begins, the path and acceleration limits, the liquid-entry point, the required immersion depth, permitted swing, dwell time, withdrawal profile and the condition in which the load may travel again. A single maximum hoist speed does not prove that the cycle can be achieved.

    1. Pickup and confirmation: verify fixture engagement, gross load and permission to leave the furnace zone.
    2. Transfer: use the approved bridge, trolley and hoist profile while controlling sway and clearance.
    3. Immersion: transition to the specified lowering mode and reach the defined depth within the treatment window.
    4. Bath dwell: hold or move the load only as permitted by the recipe, tank agitation and fixture design.
    5. Withdrawal and drainage: recover at the defined speed, stop at the drainage position and contain liquid before travel.
    6. Completion and traceability: release the route only after the load, tank and downstream station meet the agreed conditions.
    automated metallurgical crane controls applicable to heat treatment line integration
    Cycle time, safe-state logic and manual recovery are agreed with the same precision as capacity and span.

    Power-loss scenario: the specification must define the safe response before the load leaves the furnace, during transfer, during immersion, while submerged and during withdrawal. Emergency power, redundant functions or a manual recovery arrangement are selected from the process risk assessment and site infrastructure.

    Bath Media, Heat, Vapor and Corrosion Protection

    Workpiece temperature is not the same as crane ambient temperature. Thermal design uses exposure at each component, including radiation from the load and furnace, hot vapor above the bath, splash, air movement and the time spent in each zone.

    Process Medium Crane Interface to Define Project Measures to Evaluate
    Water Steam plume, splash, condensation and retained water Drainage, corrosion system, enclosure and cable selection, visibility and ventilation
    Polymer Solution Concentration, residue, compatibility and cleaning method Material compatibility, wash-down boundaries, slip control and maintenance access
    Brine Salt mist, splash and accelerated corrosion Protective coating, stainless or protected hardware where justified, sealed equipment and inspection intervals
    Oil Vapor, mist, surface contamination and fire risk Site fire strategy, ventilation, electrical-area review, emergency response and contamination control
    high-temperature bridge crane environment used as an adjacent thermal engineering reference
    High-temperature crane experience is relevant to thermal protection, but the heat-treatment bath adds its own vapor, splash, corrosion and emergency conditions.

    Oil Quenching Requires a Site-Specific Fire Review

    Oil type, flash characteristics, bath temperature, vapor control, ignition sources, fire detection, suppression, ventilation and emergency procedures are defined by the process owner and applicable local requirements. Electrical-area classification and equipment selection follow that review; they should not be assumed from the word “oil” alone.

    The crane supply boundary should state who provides the tank cover, ventilation, fire system, process sensors, emergency power, cable interfaces, containment and final integrated test.

    Attachments, Fixtures and Load Orientation

    Baskets and Racks

    Define empty and loaded mass, support points, deformation limits, liquid flow, drainage, center of gravity, maximum temperature and positive engagement.

    Lifting Beams and Spreaders

    Confirm hook spacing, headroom, load equalization, hot-zone exposure, proof testing, storage position and compatibility with every approved load family.

    Tongs and Clamps

    Establish the gripping principle, acceptable surface contact, engagement confirmation, loss-of-force response and behavior at process temperature.

    Vertical Lifting Fixtures

    Control long-load alignment, lateral stability, tank clearance and pickup verification through the full lift and immersion depth.

    Dual-Point Suspension

    Specify capacity split, permitted tilt, synchronization tolerance, load sharing, reeving behavior and the response to unequal motion or sensor loss.

    Attachment Changeover

    Plan storage, identification, mechanical and electrical connections, interlocks, inspection status and the process for preventing the wrong attachment selection.

    Complete load path: bundle bands, temporary ties and handling aids are not treated as lifting points unless they are designed, documented and approved for that purpose. The engineered attachment must retain every component throughout transfer, immersion, agitation, withdrawal and drainage.

    Manual, Semi-Automatic and Automatic Control

    Control Level Operator Role Typical Functions Data Needed Before Quotation
    Manual Directly commands each motion from cabin or radio Variable speed, limits, overload monitoring, permissives and status display Sight lines, operator location, cycle sequence and restricted zones
    Semi-Automatic Selects a destination or cycle and supervises execution Stored positions, assisted route, automatic immersion profile and interlocks Position list, tolerance, command ownership and manual takeover rules
    Automatic Supervises production and handles exceptions Recipe routing, load tracking, anti-sway, interface handshake, diagnostics and records Functional specification, I/O list, network, cybersecurity boundary and recovery modes

    Interface Matrix

    Every exchange with the furnace, door, tank cover, agitation system, ventilation, process controller and plant network should identify the signal owner, permissive condition, timeout, fault reaction, reset authority and safe state. Automatic travel should be blocked when equipment is not in the agreed position.

    Remote access, event records, user permissions and network segregation are agreed with the plant’s operational technology policy. Automation scope includes the practical means to recover a load after a sensor, communication or drive fault.

    fully automatic overhead crane system for integrated process control
    Automatic metallurgical-crane projects provide adjacent experience in positioning, production interfaces and unmanned routes; the heat-treatment cycle still requires its own validated specification.

    Design Basis, Inspection and Acceptance

    The contract identifies the governing country, crane classification, structural and mechanism rules, electrical requirements, below-hook device standard, local registration and inspection route. Depending on destination and project requirements, the design basis may reference ISO 4301 classification; EN 13001, EN 15011 and EN 13155; or CMAA 70 with applicable ASME B30.2, B30.20 and BTH-1 provisions. Local laws and the signed specification take precedence.

    Design Review

    Approved load cases, mechanism classification, fatigue basis, runway reactions, motion profile, attachment, heat and environmental map, failure analysis and interface schedule.

    Factory Testing

    Material and fabrication records, dimensional checks, mechanism and brake tests, panel and software checks, simulated I/O, alarms, limits and document review under the agreed inspection plan.

    Site Acceptance

    Installation and alignment checks, proof and functional tests, representative fixture or load trials, process sequence, emergency response, interfaces, recovery, training and handover documents.

    Acceptance precision: “high speed,” “automatic” and “accurate positioning” should be replaced by measurable criteria—load, start and end points, elapsed time, speed profile, tolerance, repeatability, environmental condition and pass/fail method.

    Published Solution and Adjacent Project Experience

    heavy-duty high-temperature metallurgical crane platform

    YH Quenching-Crane Product Platform

    Henan Mine Crane publishes a quenching-crane platform for rapid immersion of high-temperature workpieces, with project options for thermal protection, dual braking, emergency power, manual or PLC control and automatic positioning. Published applications include steel rolls, mold steel, shafts, gears, flanges, bearing components and high-strength fasteners.

    The platform description establishes an engineering starting point. Project performance is confirmed only in the signed technical proposal and acceptance criteria.

    specialized bridge crane in a hot rolled steel production environment

    Adjacent High-Temperature and Automation References

    Published Henan Mine Crane hot-rolled steel and fully automatic metallurgical-crane projects demonstrate adjacent capabilities in heavy-duty bridge engineering, thermal environments, positioning and production-line integration.

    These adjacent references are not presented as heat-treatment deliveries. They illustrate transferable engineering disciplines; the furnace, bath, fixture and quenching cycle require separate project validation.

    Evidence boundary: product ranges on this page come from published Henan Mine Crane information. Application descriptions explain engineering routes. Adjacent project photographs show related high-temperature or automated crane work and do not represent the exact configuration offered for every heat-treatment enquiry.

    Heat Treatment Crane Price and Budget Scope

    Purpose-built heat treatment and quenching cranes are normally priced by project. A public web review completed on 20 September 2026 found specialist suppliers presenting these cranes through request-for-quotation pages rather than comparable numeric prices. No credible like-for-like public price was found for a complete quenching-crane system with a defined load, immersion cycle, bath medium, emergency strategy and delivery scope.

    A reviewed marketplace page listed an ordinary double-girder overhead crane at US$15,000 per set. The listing described a general workshop or warehouse crane, not a heat-treatment duty, and is therefore not a dependable budget for a quenching system. A valid comparison must normalize the technical and commercial scope.

    Market Reference Published Price Status How to Use It
    Specialist Heat-Treatment or Quenching Crane Project quotation / RFQ Obtain a configuration-based proposal against one common duty specification
    Public Specialist Platform Pages Capacity and dimensional ranges published; numeric price generally not published Useful for identifying available engineering envelopes, not for installed-project budgeting
    Ordinary Double-Girder Marketplace Listing US$15,000 per set in one reviewed listing General workshop or warehouse duty; do not compare directly with a quenching crane
    Henan Mine Crane Heat Treatment System Project quotation Price follows approved process, crane, attachment, interface and supply-boundary data

    Main Cost Drivers

    Crane and Runway
    Capacity, span, lift, wheel loads, structure, mechanisms, rails and building modifications.
    Process Performance
    Immersion profile, duty, brakes, redundancy, emergency power, positioning and availability.
    Attachment and Environment
    Basket, fixture or beam; heat protection; corrosion system; enclosures and special materials.
    Controls and Interfaces
    Cabin or radio, PLC, anti-sway, sensors, automation, plant networks and traceability.
    Delivery Scope
    Freight, taxes, erection, electrification, commissioning, testing, training, spares and documentation.
    Compliance Route
    Destination standards, third-party inspection, local registration and documentation language.

    Comparable quotation rule: issue the same load matrix, motion cycle, bath data, duty, layout, standards and supply boundary to every supplier. Require explicit inclusions, exclusions, utilities, interface responsibilities, testing scope, spare parts and commercial terms.

    Information Required for a Heat Treatment Crane Quote

    A complete enquiry allows the crane structure, hoist, attachment, thermal protection, emergency response, controls, runway reactions and commercial scope to be priced on the same basis.

    Workpiece and Fixture

    Minimum, normal and maximum mass and dimensions; material; temperature at pickup; center of gravity; orientation; basket, rack, spreader or clamp data; drawings and photographs.

    Treatment Cycle

    Furnace pickup point, route, maximum transfer time, immersion depth and profile, dwell, agitation, withdrawal, drainage, destination, cycles per hour and load spectrum.

    Tank and Environment

    Bath medium and temperature; tank dimensions and freeboard; covers and agitation; vapor, splash and ventilation; furnace and ambient heat data; corrosion and fire strategy.

    Workshop and Runway

    Rail-center span, runway length and elevation; required lift; headroom; approaches; rail and beam data; wheel-load limits; cross-section, equipment layout and installation access.

    Controls and Emergency Strategy

    Manual, assisted or automatic mode; positions and tolerances; interface signals; cameras; anti-sway; power-loss response; emergency source; recovery access and safe states.

    Commercial and Compliance Scope

    Destination, power supply, standards, inspection route, Incoterm, freight, installation, electrification, commissioning, testing, training, spares, documentation and warranty requirements.

    Fastest route to a comparable proposal: provide the workshop cross-section, equipment plan, workpiece and fixture matrix, second-by-second treatment sequence, bath data and required supply boundary. Unknown items can be listed as open points, provisional allowances or exclusions.

    Frequently Asked Questions

    Is a heat treatment crane the same as a quenching crane?

    A quenching crane is one type of heat treatment crane. It is specifically engineered for timed immersion and recovery. Heat-treatment handling can also include furnace transfer, tempering, annealing and cooling operations without rapid immersion.

    How is heat treatment crane capacity calculated?

    Start with the heaviest workpiece and add the basket, fixture, beam, rigging, hook block, retained liquid and every suspended accessory. Then evaluate eccentric loading, multi-point load sharing, dynamic motion and abnormal cases.

    Can a standard overhead crane perform quenching?

    Only if a dedicated engineering review confirms the complete process. Immersion time, hoist profile, brakes, power-loss response, thermal exposure, vapor, splash, corrosion, fixture, clearance and duty can require a purpose-built system.

    Which quenching media can the crane serve?

    Water, polymer solution, brine and oil can be considered. Each medium creates different vapor, splash, corrosion, contamination, ventilation and fire conditions, so the bath data and site risk assessment are required.

    How much does a heat treatment crane cost?

    Specialist suppliers normally quote by project, and the September 2026 public review found no dependable like-for-like numeric price. Capacity, immersion performance, attachment, environment, redundancy, automation, runway and installed scope must be defined first.

    What happens if power fails during quenching?

    The required response is defined for every cycle stage. Depending on the risk assessment, the solution may use emergency power, selected redundant functions, controlled recovery and a documented manual procedure.

    Can the crane integrate with furnaces and tank controls?

    Yes. Integration can include door, cover and agitation interlocks, route permissions, load identification, recipe selection, position confirmation, event records and plant-system communication under an approved functional specification.

    What should be tested before handover?

    Tests cover rated and proof loads, brakes, limits, overspeed and overload functions, process motion, positioning, attachment, interfaces, safe states, emergency response, manual recovery and representative treatment sequences.

    Request a Heat Treatment Crane Quote

    Submit the workpiece and fixture matrix, pickup temperature, furnace-to-bath sequence, transfer and immersion timing, bath medium and dimensions, duty cycle, span, lift, runway data, control level, power-loss strategy, destination and supply boundary. Henan Mine Crane will prepare a configuration-based technical and commercial proposal.
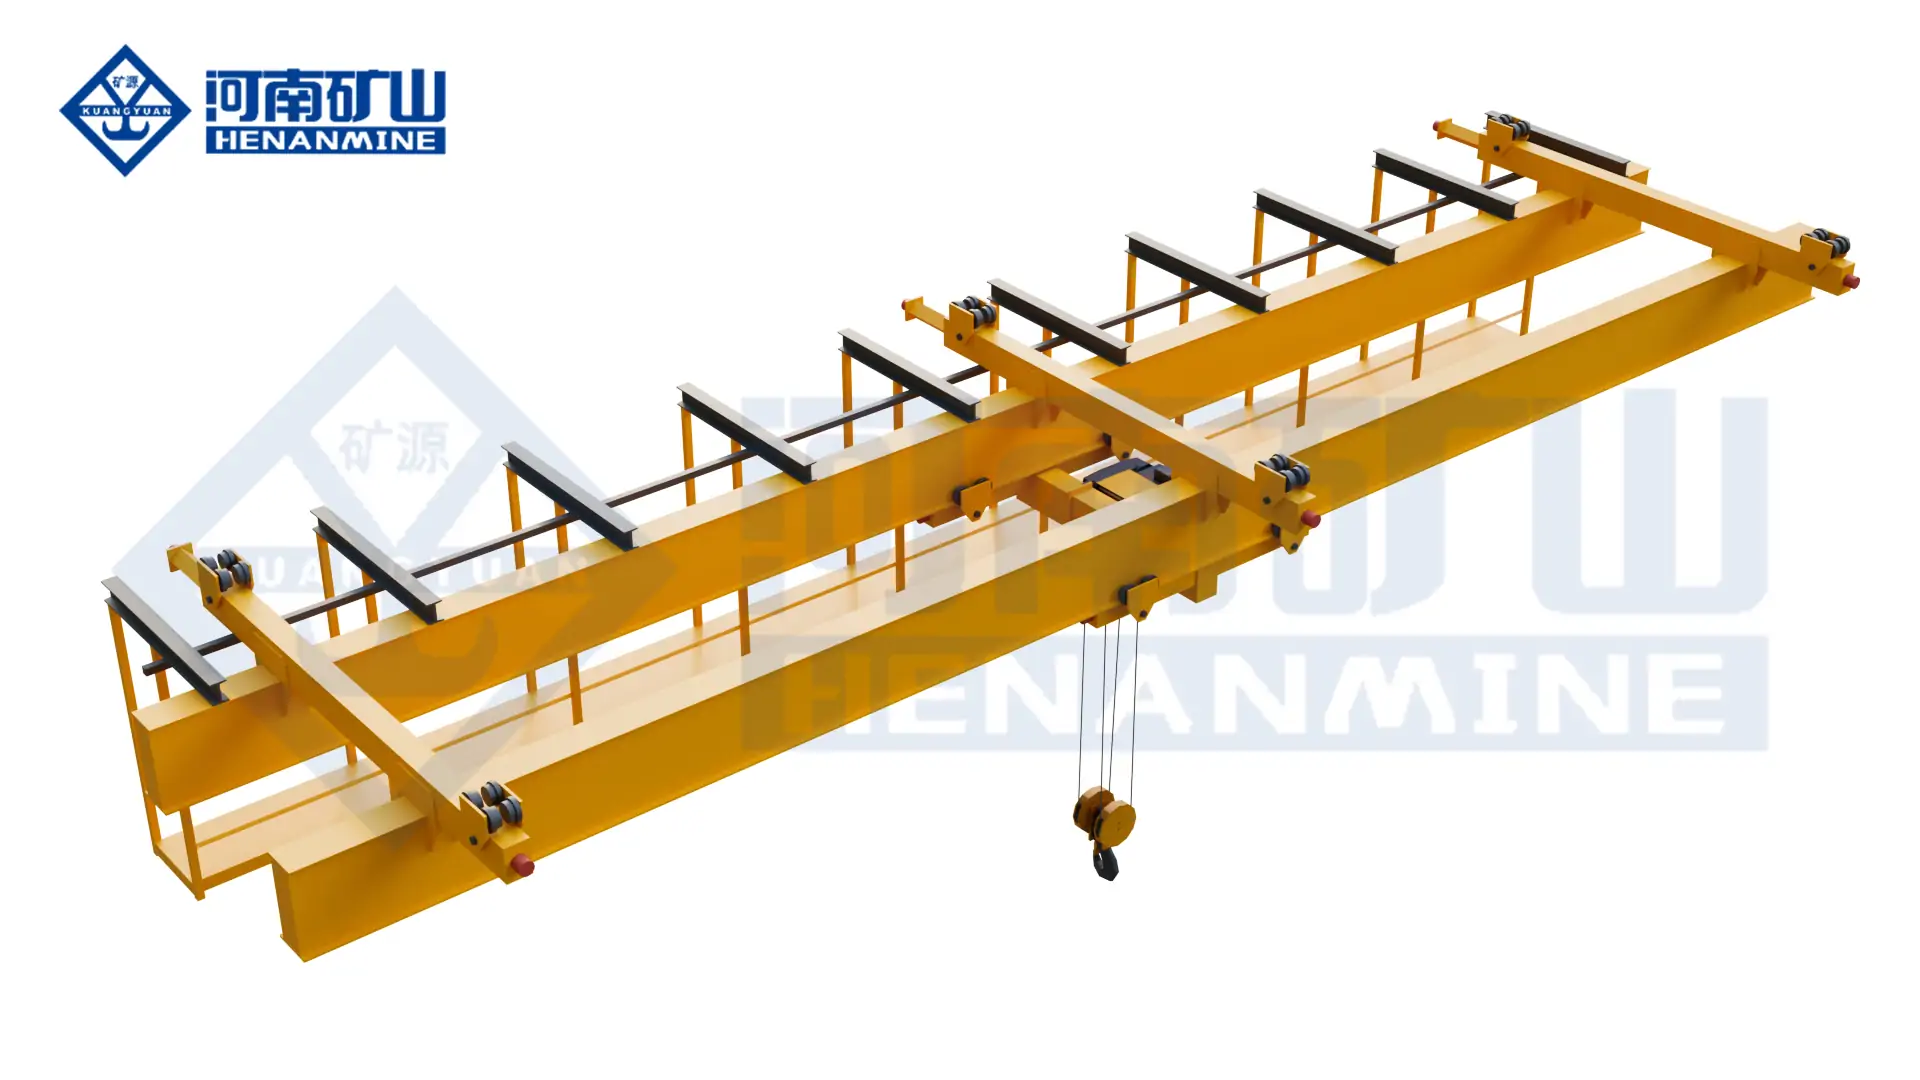
    Henan Mine CraneDiscuss your requirements ↗