Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

Blog

  • When a Standard Crane Needs Customisation: A Site Review Checklist

    When a Standard Crane Needs Customisation: A Site Review Checklist

    Technical guide

    When a Standard Crane Needs Customisation: A Site Review Checklist

    Customisation is most useful when it resolves a defined operating constraint. Use the load, building geometry and handling sequence to identify which changes belong in the specification and which requirements still need confirmation.
    Henan Mine CraneTechnical guide · Updated 2026Crane selection, project scope and operating requirements
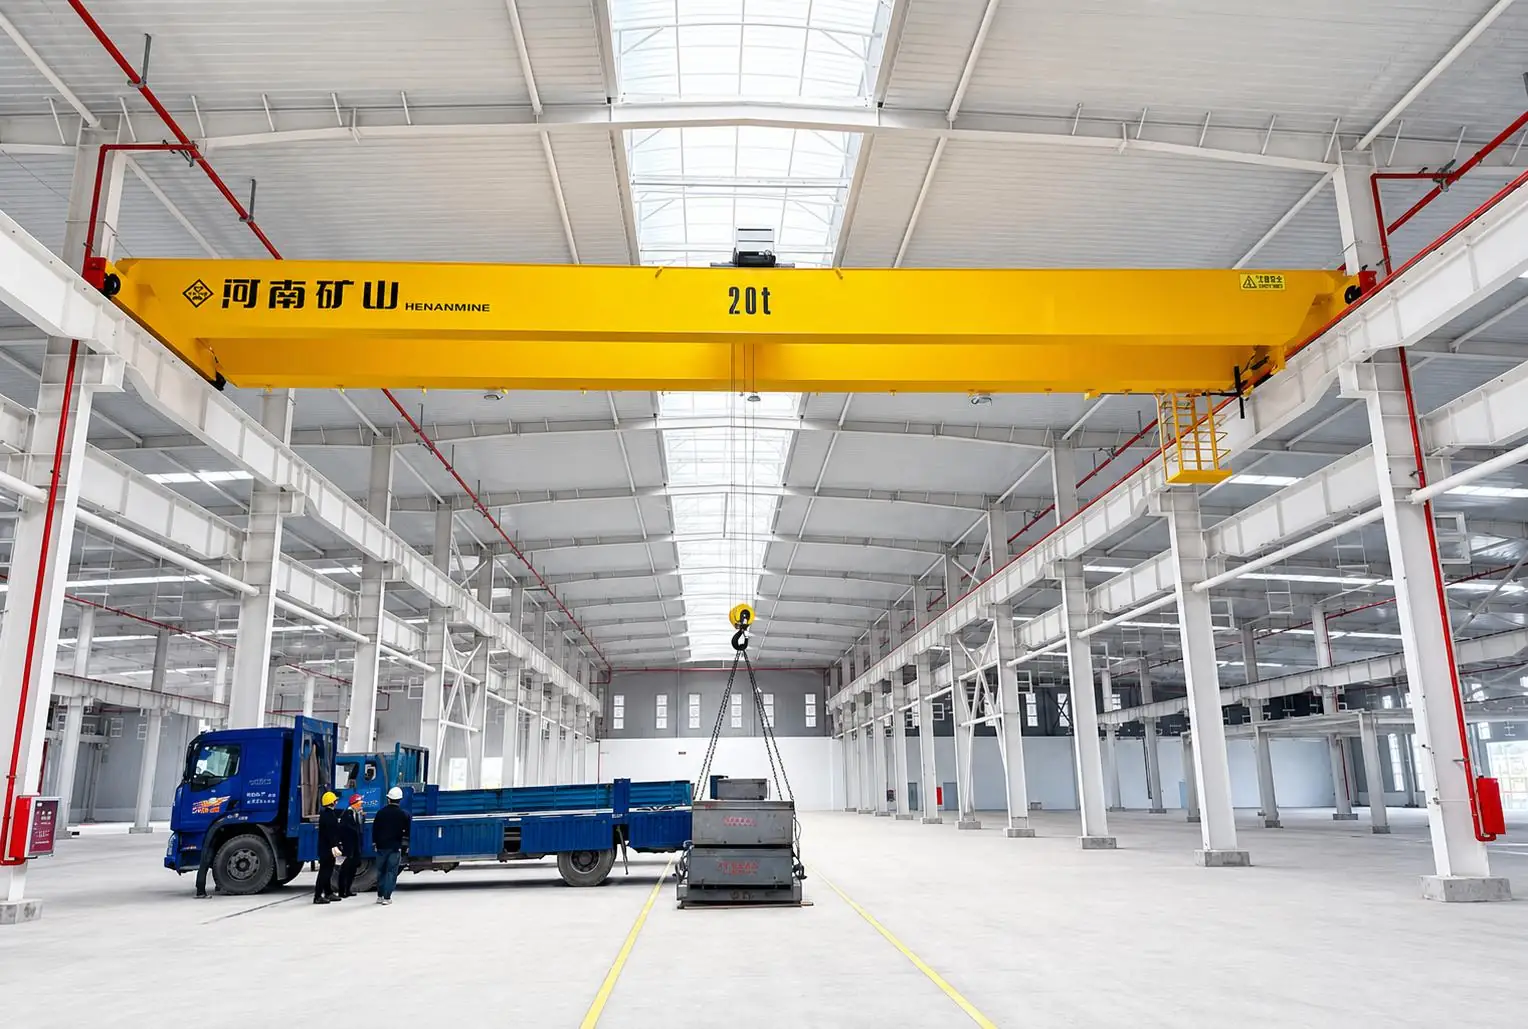
    Henan Mine Crane overhead crane inside a workshop bay
    Henan Mine Crane overhead crane inside a workshop bay
    Project planning notes

    Key points for this crane project.

    1. What Is a Custom Crane and When Is It Needed?
    2. 10 Warning Signs You Need a Custom Crane
    3. Custom Crane vs. Standard Crane: Which Is More
    Read the technical guide

    What Is a Custom Crane and When Is It Needed?

    Customized cranes are non-standard industrial lifting equipment specially designed, individually configured, and optimized by crane manufacturers based on the actual working conditions, site conditions, load parameters, operating requirements, and environmental characteristics of the user's site. Different from mass-produced standard lifting equipment, customized bridge cranes and gantry cranes are not limited to fixed parameters, fixed structures, and fixed configurations. They can be adapted to various special, extreme, and complex industrial hoisting scenarios, and are widely used in high-end fields such as new energy, chemical industry, metallurgy, ports, heavy industry manufacturing, and special engineering.

    Standard vs. custom crane

    Standard industrial cranes are general-purpose mass-produced models in the industry. The parameters, structure, configuration, and dimensions are all standardized. The span, lifting height, rated load, operating speed, and protection level are all fixed and unified. They are mainly suitable for conventional factories, ordinary material hoisting, and low-frequency operation scenarios. Its core advantages lie in sufficient stock, short delivery cycle, low initial procurement cost, universal accessories, and convenient maintenance. It is suitable for the general hoisting needs of most small and medium-sized enterprises.

    Henan Mine Crane manufactured customized port cranes are one-to-one exclusive design models, all parameters can be adjusted as needed, and the structure, material, control system, protection configuration, and operating logic can be adapted to on-site working conditions. Although the initial procurement cost is slightly higher and the design and production cycle is longer, the fit, operating stability, operating efficiency, and safety factor of the equipment far exceed the standard model, which can solve the problems of various working conditions that cannot be adapted to standard lifting equipment, and eliminate the problems of idle equipment, retrofit and rework, failure and shutdown from the root cause.

    When customization adds value

    Crane customization is not a blind upgrade, but a targeted selection method to solve production pain points and create long-term value. When enterprises face the needs of restricted sites, special loads, harsh environments, high-frequency operations, and automated production, the value of customized transformation and exclusive industrial cranes will be fully highlighted.

    The core value of customization is reflected in four dimensions. The second is the value of efficiency, matching exclusive operating parameters, adapting to high-frequency, heavy-duty, and special material hoisting, greatly improving production efficiency. Third, the safety value, targeted configuration of explosion-proof, anti-corrosion, high temperature resistance, anti-overload and other special functions, to avoid safety hazards in extreme working conditions. The fourth is the cost value, which reduces the hidden costs of long-term downtime, maintenance, transformation, and replacement of lifting equipment, and lengthens the service life of the equipment.

    10 Warning Signs You Need a Custom Crane

    Many equipment selection errors in enterprises are essentially ignoring the special signals of working conditions and forcibly adapting standard lifting equipment to non-standard scenarios. The following 10 core warning signals, as long as any one is met, it means that your working conditions are no longer suitable for standard models. Customized industrial cranes are a more scientific, economical and safer choice.

    Required capacity exceeds standard models

    The rated load of standard cranes has strict industry fixed gears, covering conventional light, medium and heavy lifting needs, but for oversized tonnage and unconventional heavy-duty lifting scenarios, the upper load limit of standard models cannot meet the operating requirements. If the weight, combined load, and dynamic load of the materials that need to be hoisted in your production operation exceed the parameter range of all standard lifting equipment, forced use of standard equipment will cause overload operation, structural deformation, insufficient safety factor, etc., which can easily cause safety accidents. At this time, it is necessary to optimize the main girder structure, travel mechanism, and lifting system through customized design to create a high-capacity exclusive industrial crane to match the needs of heavy-duty operations.

    Span or lift height is unusual

    The span and lifting height of the standard crane are all fixed standardized dimensions, which are suitable for general plant construction specifications. However, many old factories, customized production workshops, and outdoor engineering sites will have non-standard spans and ultra-high/ultra-low lifting requirements. For example, in scenarios where the span of the plant is between two standard gears, ultra-high lifting and hoisting of high-altitude equipment is required, and the height of the fuselage needs to be reduced in low-rise plants, the standard equipment either cannot be installed or the scope of operation is limited. Customized cranes can accurately customize the span and lifting height on demand, adapt to non-standard size scenarios, and maximize the use of working space.

    Working space has clearance limits

    Some production workshops have space limitations such as dense beams and columns, narrow top space, limited passages on both sides, and compact equipment layout. The size of the standard crane fuselage, the reserved clearance for operation, and the fixed end beam structure are very prone to colliding with the structure of the plant, unable to pass normally, and the blind area of the operation is too large. Customized special cranes for small spaces can optimize the fuselage structure, compress the end size, adjust the layout of the lifting mechanism, reduce the safety gap, and complete the complete hoisting operation in a limited space. It is perfectly adapted to small and complex work sites and solves the equipment adaptation problems caused by space constraints.

    Crane duty cycle is extremely high

    Ordinary standard cranes are designed for low-frequency, intermittent hoisting operations, and cannot be adapted to the high-load conditions of assembly line matching, continuous production, and 24-hour uninterrupted operation. In heavy industry manufacturing, assembly line production, port loading and unloading scenarios, cranes start and stop frequently, run continuously, and switch loads frequently. Standard equipment will quickly experience wear and aging, motor overheating, component fatigue, frequent failures and shutdowns. Henan Mine Crane manufactured customized high-work port cranes, which can be upgraded with high-strength wear-resistant parts, high-power adapted motors, enhanced transmission and braking systems, and adapted to ultra-high operating frequencies to meet the needs of continuous operation around the clock, greatly reducing the probability of failure and shutdown.

    Loads require special handling

    Standard spreaders and standard operating logic can be used for hoisting conventional steel, materials, and boxes, but for special loads such as flammable and explosive, precision instruments, high-temperature castings, ultra-long and ultra-wide special-shaped components, and vulnerable materials, standard lifting equipment cannot achieve safe and stable hoisting. Customized cranes under special working conditions can be equipped with exclusive spreaders, fine-tuning the lifting speed, adding sway control, precise positioning, and smooth start and stop functions, supporting slow alignment, micro-speed fine-tuning, and anti-impact hoisting, and adapting to the refined and safe operation requirements of special materials to avoid material damage, hoisting offset, and falling risks.

    Operating environment is challenging

    Conventional workshops at room temperature, dryness and dust-free are suitable scenarios for standard cranes, while harsh environments such as chemical industry, metallurgy, mines, ports, alpine, high temperature, dust, humidity, and corrosive gases can quickly corrode and damage the electrical and metal structures and transmission components of standard cranes. Customized anti-corrosion and explosion-proof cranes can be targeted for protection according to environmental characteristics: high-temperature-resistant materials and heat dissipation systems are used in high-temperature environments, low-temperature environments are adapted to low-temperature-resistant electrical components and lubrication systems, and corrosive environments are multi-layer anti-corrosion spraying and sealing treatment. The explosion-proof area is equipped with a full set of explosion-proof electrical equipment, which is fully adapted to complex and harsh working conditions.

    Custom Crane vs. Standard Crane: Which Is More Cost-Effective?

    Most buyers believe that standard industrial cranes are more economical. The core is to only focus on the initial purchase price and ignore the whole life cycle cost of the equipment. In fact, the core of cost-effectiveness lies not in the single purchase price, but in adaptability, stability, operation and maintenance costs, service life and production gain. For non-standard complex working conditions, the comprehensive price ratio of customized lifting equipment is much higher than that of standard models.

    Initial cost vs. lifecycle cost

    At the initial procurement cost level, standard cranes are mass-produced in bulk, the technology is mature, and there is no need for exclusive design. The purchase price is lower and the delivery speed is faster. Customized cranes require exclusive design, customized production, and special testing. The initial procurement cost is slightly higher and the delivery cycle is relatively longer. At the cost level of the whole life cycle, customized non-standard lifting equipment has significant advantages. Customized equipment adapted to working conditions has an extremely low failure rate, slow wear rate, and longer service life, without frequent maintenance and replacement of accessories. At the same time, there is no need to transform the factory building, no need to compromise the production process, and the production efficiency is steadily improved.

    Downtime and maintenance considerations

    Standard cranes operate under non-standard operating conditions, and the speed of component loss will increase exponentially. Motors, brakes, main beams, and travel mechanisms are prone to failure. Frequent downtime and maintenance will directly interrupt the production process, resulting in high production losses. Moreover, under non-standard working conditions, the loss of standard equipment accessories is special, the adaptability of general accessories is poor, the maintenance is difficult, and the waiting period is long. Customized industrial cranes are specially designed based on working conditions, with component selection, structural strength, and operating parameters that exactly match the requirements of the operation, uniform wear, extremely low probability of failure, and greatly reduced frequency of operation and maintenance. At the same time, manufacturers will support exclusive maintenance plans and customized accessories systems, which are efficient and convenient for maintenance, minimize downtime and ensure production continuity.

    When partial customization is enough

    Not all non-standard working conditions require a customized crane for the whole machine. If the site, load, and basic operating parameters meet the requirements of the standard model, there are only local functional shortcomings, and local customization can meet the needs, taking into account cost performance and adaptability. Common local customization includes: installing explosion-proof, anti-corrosion, sway control, intelligent monitoring modules, upgrading the electronic control system, replacing exclusive spreaders, fine-tuning the operating speed, and optimizing the protective structure. Local customization has low cost and fast delivery, and can quickly fill the functional shortcomings of standard lifting equipment, which is suitable for scenarios with small differences in working conditions.

    How to Specify a Custom Crane

    The selection specifications of customized cranes directly determine the adaptability, safety and practicality of equipment. The scientific customized selection process can effectively avoid problems such as design deviations, inconsistent parameters, and functional redundancy, and ensure that customized industrial lifting equipment accurately matches on-site working conditions.

    Define load and duty requirements

    The first step in customizing the design of Henan Mine Crane manufactured crane is to accurately define the load and operating condition parameters, covering key indicators such as rated lifting weight, maximum dynamic impact load, material shape and size, daily lifting frequency, equipment working system level, daily operating time and start-stop frequency. Accurately defining the load range and operating intensity is the core basis for equipment structure design, core component selection, and motor power matching. It can effectively avoid the cost waste caused by insufficient load and inability to put into production or excessive design, and ensure the long-term stable adaptation of customized lifting equipment to the production rhythm.

    Measure site and runway conditions

    In the pre-survey stage of customized cranes, it is necessary to accurately measure the site and runway working condition data in all directions, including the effective span of the plant, the maximum lifting height, the top clearance size, the overall length and width of the site, the runway track gauge, the load-bearing limit of the track, the structural parameters of the cow leg, the installation point of the equipment and the scope of the blind spot of the operation. Accurate and comprehensive site data can provide reliable support for fuselage size optimization, travel mechanism configuration, installation plan and span customization to ensure smooth on-site installation of customized industrial cranes, no caton operation, and full adaptability.

    Identify environmental requirements

    Comprehensive investigation and combing of the environmental conditions of the operation site is a key part of custom-made cranes. It is necessary to verify the environmental temperature and humidity, dust concentration, whether there are corrosive gases, flammable and explosive media, and take into account the special working conditions such as open-air rain and snow, seaside salt spray, high cold and high temperature. According to different environmental characteristics, the equipment protection level, main material, anti-corrosion spraying process, explosion-proof configuration and high and low temperature resistance structure design are determined in a targeted manner to effectively resist environmental erosion, greatly extend the service life of customized lifting equipment, and ensure stable operation around the clock.

    Confirm controls and safety functions

    It is necessary to combine the actual production process and operation needs of the enterprise to determine the control mode of the crane, covering various methods such as ground operation, wireless remote control, manual control, automated operation and remote linkage. At the same time, it is equipped with a complete set of safety protection functions on demand, including overload protection, travel limit, anti-collision, sway control, emergency braking, fault alarm, intelligent monitoring and lightning protection devices. The perfect control system and safety configuration can avoid hoisting risks in all directions and ensure the safe, efficient, intelligent and stable operation of customized industrial cranes.

    When Should You Choose Custom Engineering?

    There is no need to blindly follow the trend in crane selection, the core is to fit its own working conditions. Combining the adaptation scenarios of standard equipment and customized equipment, the selection plan can be accurately judged, so that the selection of industrial lifting equipment can maximize cost performance and practicality.

    Standard crane fits the application

    For standardized plant scenarios that are dry at room temperature, dust-free and corrosion-free, light, medium-load, low-frequency intermittent hoisting of ordinary steel and finished materials, and when enterprises pay attention to budget control and pursue rapid equipment delivery and commissioning, standard cranes are preferred. It is most suitable. This type of mass-produced industrial crane has mature technology, stable technology, high market penetration rate, convenient procurement of general accessories, simple and worry-free daily operation and maintenance, and can meet the basic hoisting needs. Under the premise of saving procurement and operation and maintenance costs to the greatest extent, and adapting to conventional industrial production conditions.

    Custom crane is technically necessary

    When there are special needs such as oversized loads, non-standard span and lifting height, narrow working space, high-frequency continuous operation, special material hoisting, harsh working conditions, etc. on the site, or when multi-mechanism synchronous linkage and intelligent unmanned control functions are required, standard cranes cannot be fully adapted. Forced use will cause a series of problems such as equipment failure, production downtime, and safety hazards, resulting in high hidden costs. At this time, the customized crane of the whole machine has the technical necessity to fully fit the exclusive working conditions, solve the problem of equipment adaptation from the root cause, and ensure the safe and efficient operation of production.

    Partial customization is the better option

    If the plant site, hoisting load, and basic operating parameters are fully adapted to the standard crane model, there are only local shortcomings such as protection performance, intelligent control, and exclusive operating functions, and there is no need for customized transformation of the whole machine. It is most reasonable to choose a locally customized optimization method. Anti-corrosion, explosion-proof, sway control, and intelligent monitoring modules can be installed in a targeted manner, and the electronic control system and special spreaders can be upgraded to make up for equipment shortcomings with extremely low transformation costs and extremely fast delivery speeds, taking into account the adaptability and economy of the equipment. It is a cost-effective lifting equipment upgrade plan optimized for small and medium-sized working conditions.

    Henan Mine Crane

    Henan Mine Crane has been deeply engaged in the field of lifting equipment for many years, and has mature non-standard customized R&D and production capabilities. It can be accurately adapted to various complex and extreme industrial hoisting conditions, and perfectly solves the problems of poor adaptation, many failures, and high operation and maintenance costs of standard industrial cranes. Henan Mine Crane Factory can provide a full range of customized bridge and gantry cranes and one-stop landing services, covering multi-industry production scenarios, professional survey and design, precision production, on-site installation and maintenance throughout the process, to help enterprises produce efficiently and safely. If you need it, you can get exclusive customized solutions and quotations for free.

    Discuss the crane arrangement for your project.

    Customisation is most useful when it resolves a defined operating constraint. Use the load, building geometry and handling sequence to identify which changes belong in the specification and which requirements still need confirmation. Share the load, available drawings, working cycle and site conditions with Henan Mine Crane so the required configuration and supply boundary can be discussed.

    Related crane configurations

    Explore crane product families and technical parameters ↗

    Updated 2026 · Henan Mine Crane
  • 400 t Intelligent Overhead Crane Dispatched for a Boiler-Manufacturing Project

    400 t Intelligent Overhead Crane Dispatched for a Boiler-Manufacturing Project

    Project Deliveries

    400 t Intelligent Overhead Crane Dispatched for a Boiler-Manufacturing Project

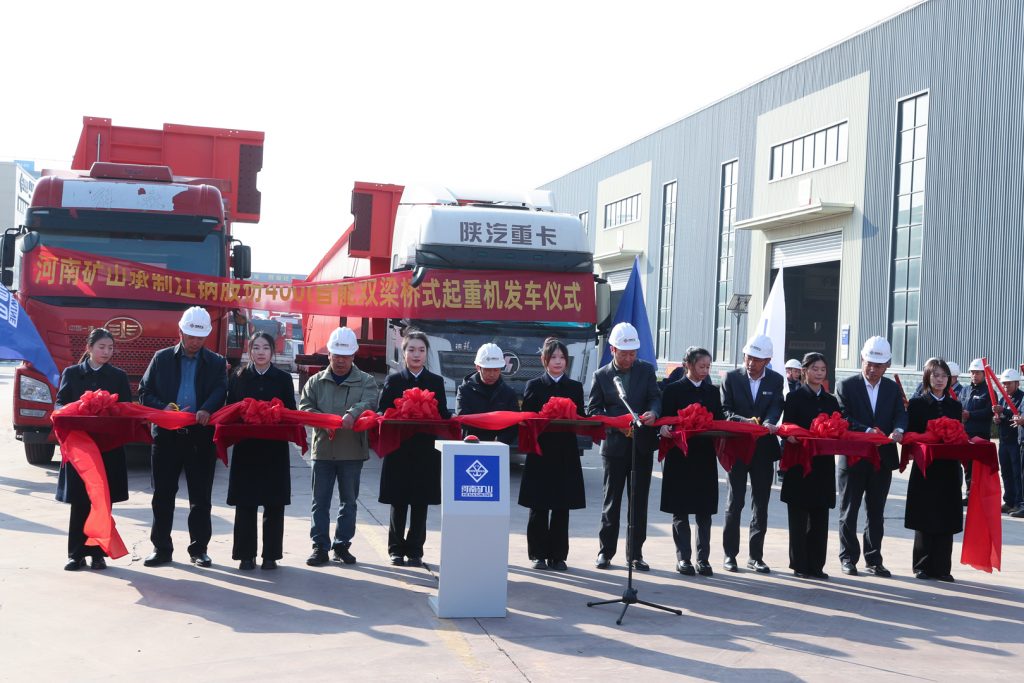
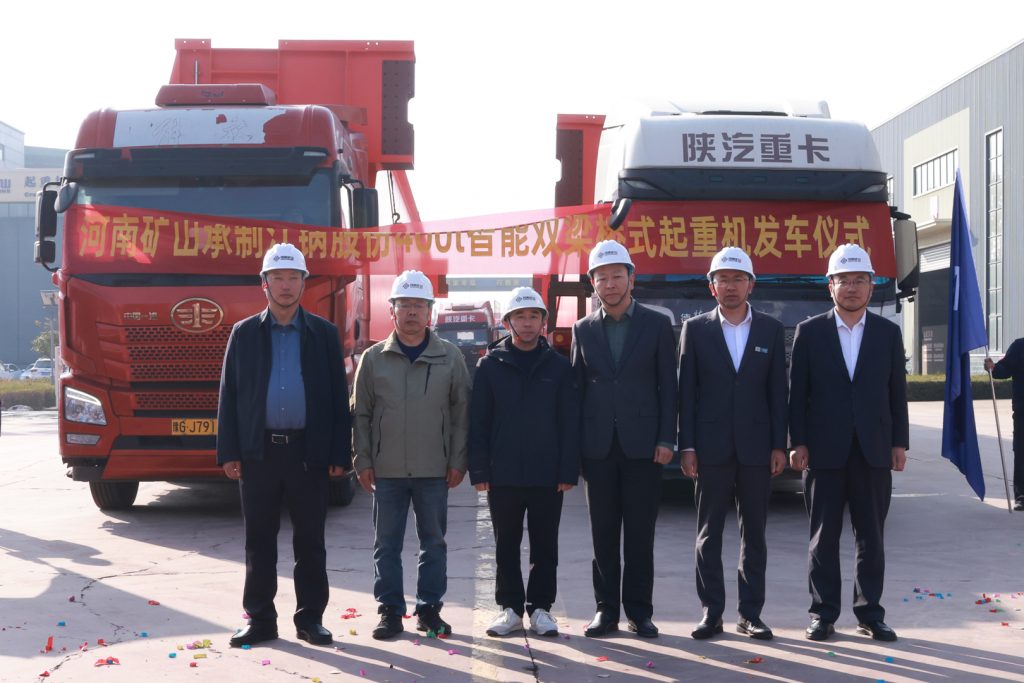
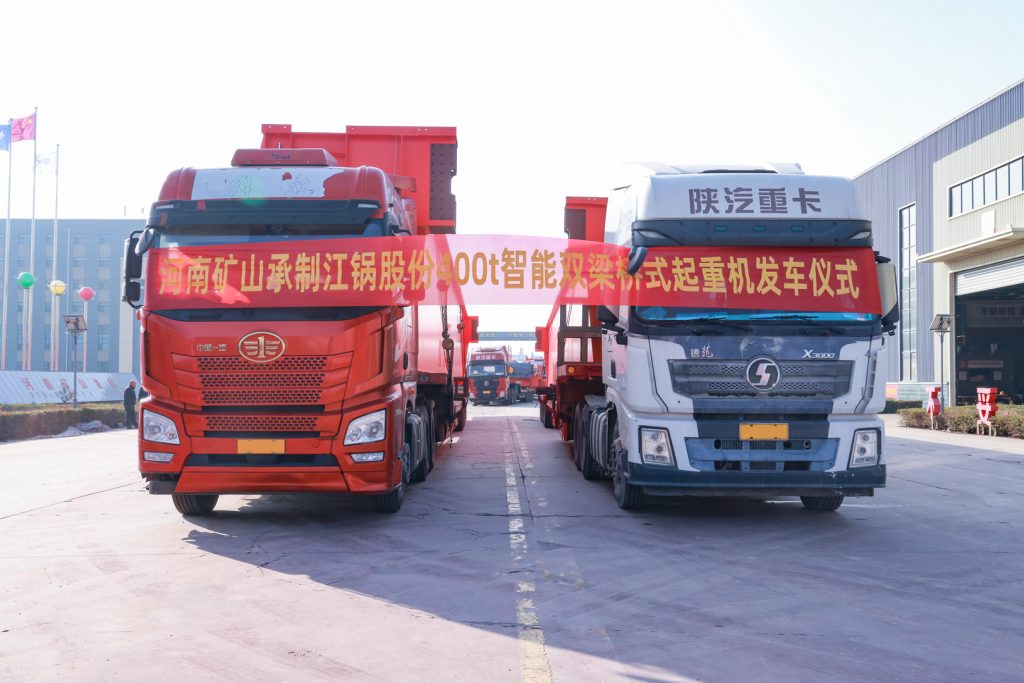
    Henan Mine Crane dispatched a 400 t intelligent double-girder overhead crane for a boiler-manufacturing customer on 15 December 2025.

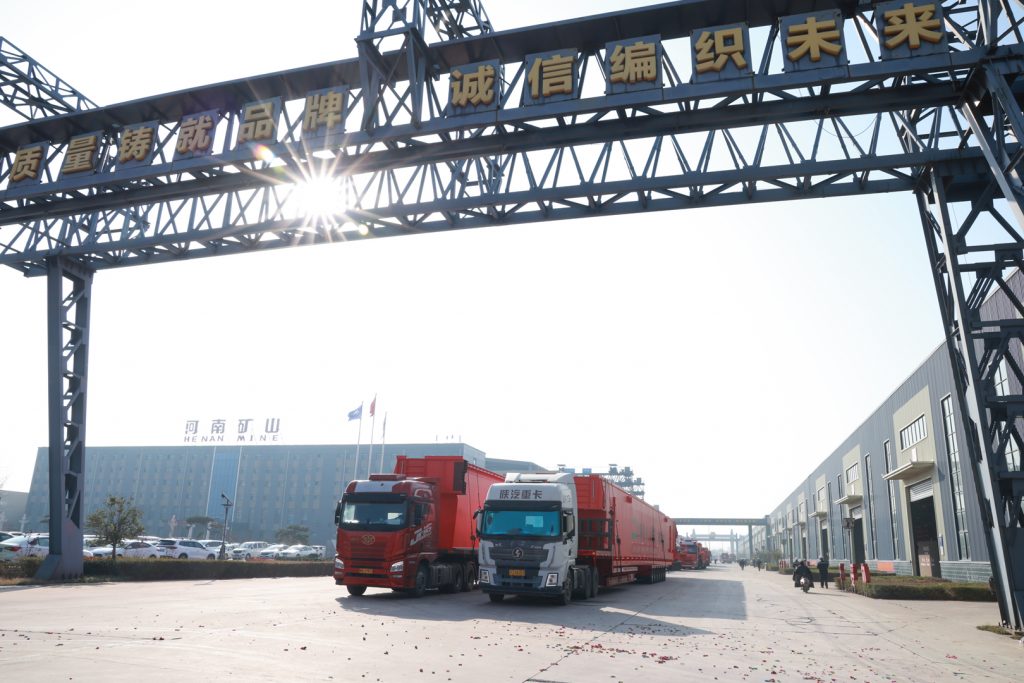
    Transport trucks carrying red crane equipment outside the factory
    Transport trucks carrying red crane equipment outside the factory.

    One crane in a larger planned equipment package

    The unit was planned to work alongside five other 400 t cranes and 17 supporting cranes. Equipment dispatch, installation and commissioning form separate milestones within the project schedule.

    Define integration and acceptance by project stage

    The crane description refers to positioning, remote operation and drive efficiency. A comparable project should specify load cases, span, lift height, controls, interaction with other cranes and the required factory and site acceptance sequence.

    Discuss your lifting requirement

    Share the lifting plan, building dimensions, crane interactions and required inspection stages for a heavy-duty crane proposal.

  • Henan Mine Crane and Yuchai Discuss Manufacturing and Supply-Chain Cooperation

    Henan Mine Crane and Yuchai Discuss Manufacturing and Supply-Chain Cooperation

    Industry & Partnerships

    Henan Mine Crane and Yuchai Discuss Manufacturing and Supply-Chain Cooperation

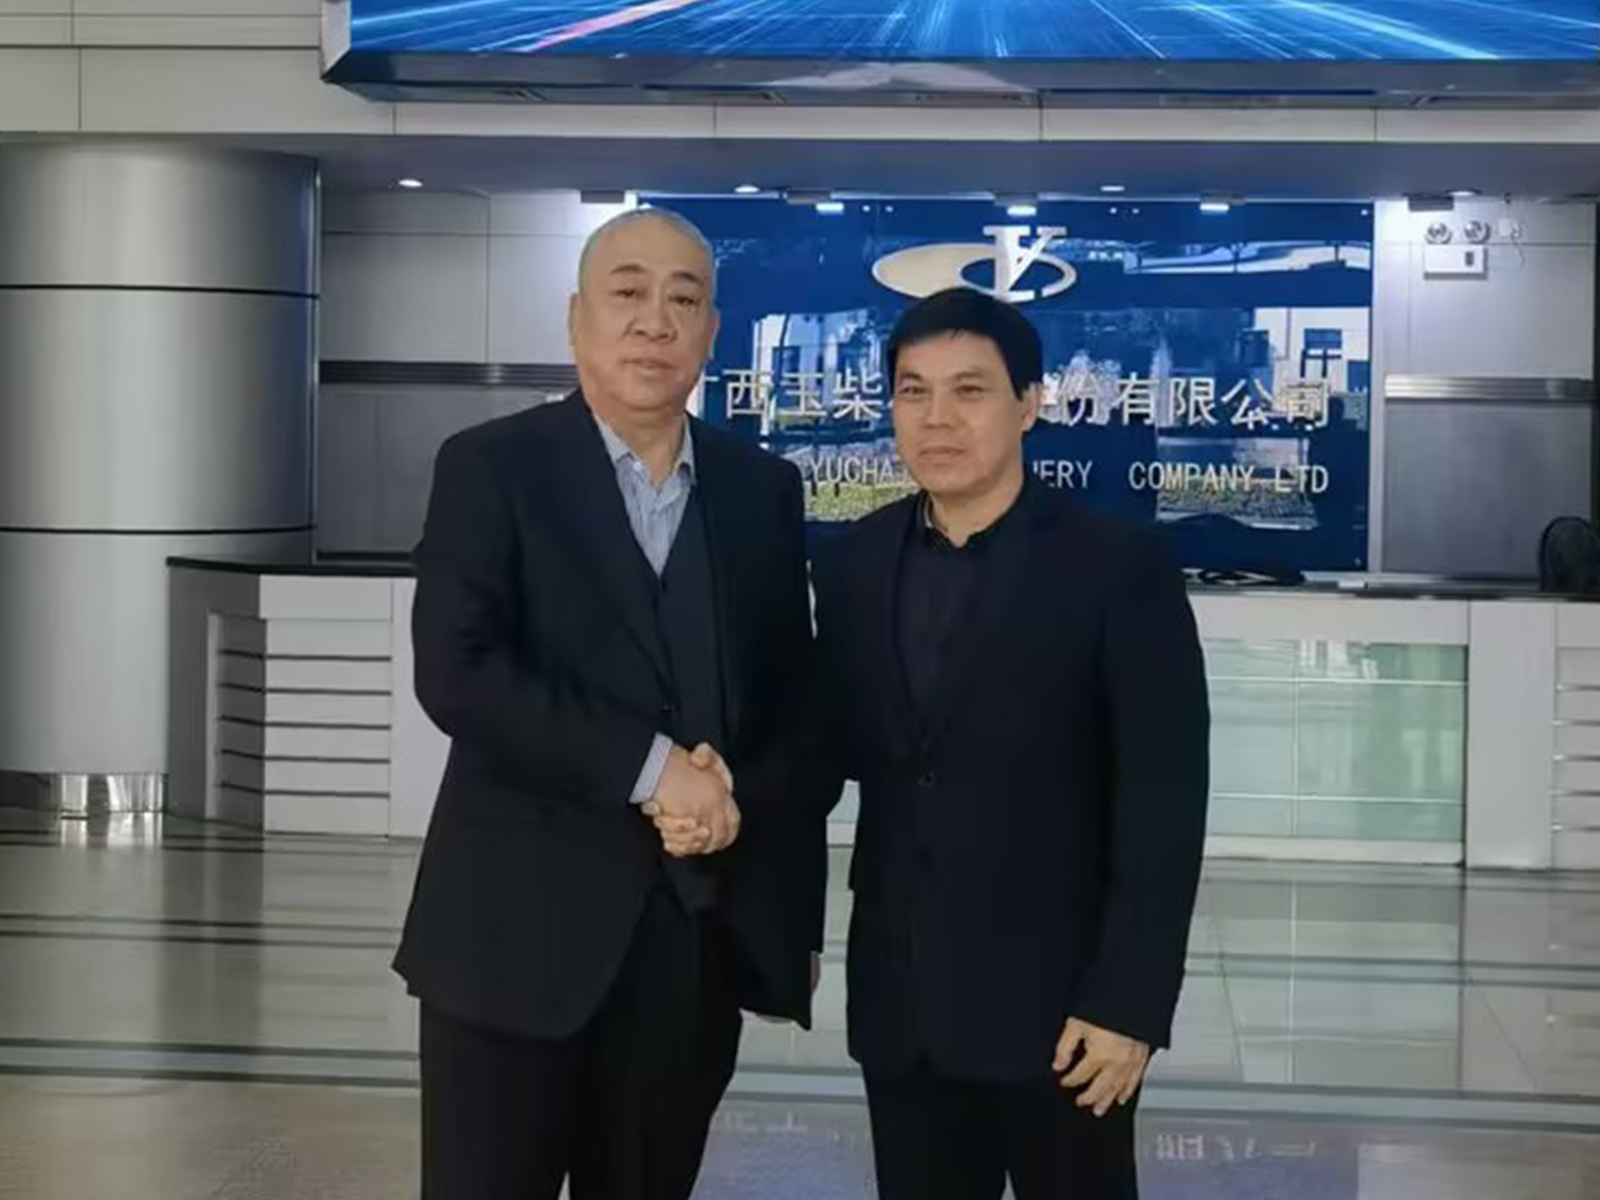
    Henan Mine Crane founder Cui Peijun visited Yuchai Group on 11 March 2026 for an exchange on manufacturing development and industrial cooperation.

    Henan Mine Crane and Yuchai representatives shaking hands
    Henan Mine Crane and Yuchai representatives shaking hands.

    Manufacturing development and industrial coordination

    The discussions addressed manufacturing upgrades and coordination across industrial and supply chains. Yuchai representatives and the visiting team exchanged views on opportunities for further cooperation.

    Contact Henan Mine Crane

    For product information, a manufacturing visit or a company enquiry, send the relevant details to our team.

  • Portal Crane Slewing Coverage: Check the Quay and Cargo Envelope

    Portal Crane Slewing Coverage: Check the Quay and Cargo Envelope

    Technical guide

    Portal Crane Slewing Coverage: Check the Quay and Cargo Envelope

    Slewing coverage should follow the vessel position, cargo transfer points and quay obstructions. Show the required working envelope on a site plan and ask the supplier to identify restricted movements and operating limits.

    Henan Mine CraneTechnical guide · Updated 2026Crane selection, project scope and operating requirements
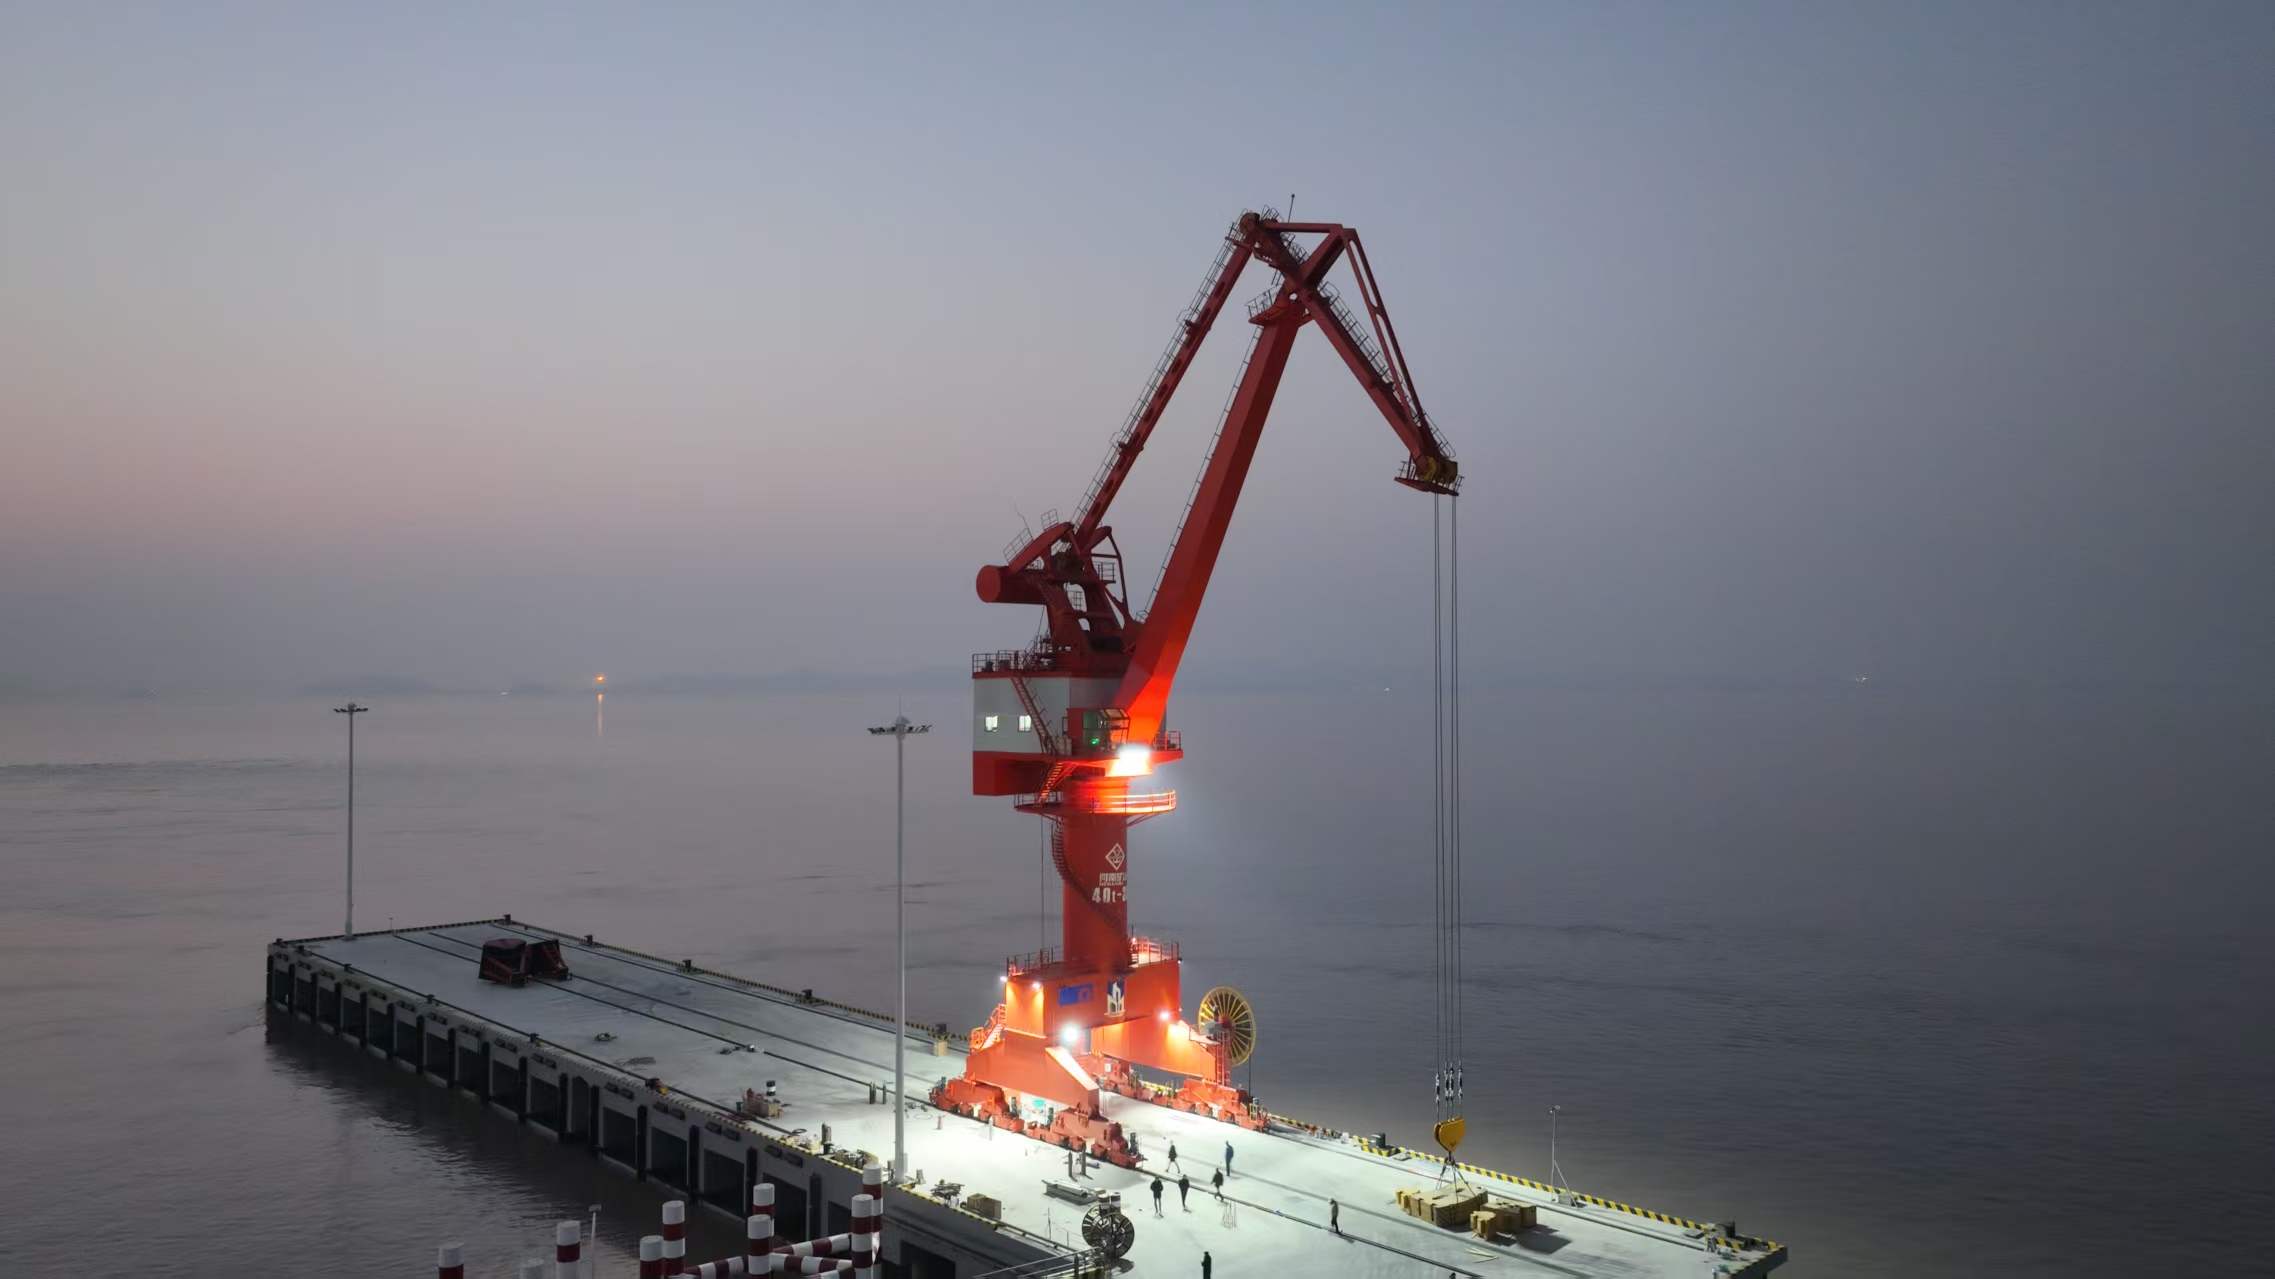
    Henan Mine Crane Portal Harbor Crane
    Henan Mine Crane Portal Harbor Crane
    Project planning notes

    Key points for this crane project.

    1. What Is the Slewing Range of a Portal Slewing Crane?
    2. Why Does Slewing Range Matter in Dock Operations?
    3. Factors That Determine the Ideal Slewing Range
    Read the technical guide

    What Is the Slewing Range of a Portal Slewing Crane?

    Definition of Slewing Range

    Slewing range is the total horizontal angle through which a crane's upper structure and boom can rotate around its vertical axis, measured in degrees. It works alongside , but is distinct from , working radius, which is the horizontal distance from the slewing center to the load, controlled by luffing the boom in or out. Slewing range defines how far around the crane can turn. Working radius defines how far out it can reach at any given rotation. The two specs are always read together on a load chart, because a crane's rated capacity at a given radius can shift slightly depending on which side of the portal the boom is slewed toward, especially on asymmetric quay layouts where one side faces open water and the other faces a fixed structure.

    Slewing angle is the term used for the specific arc a Henan Mine Crane manufactured crane is built or limited to , 180°, 270°, or 360° , while working radius is expressed as a distance, typically in meters, from the crane's centerline. Buyers sometimes confuse the two because both appear on the same specification sheet, but they answer different operational questions: slewing angle answers "which directions can the crane turn," and working radius answers "how far can it reach once turned."

    Continuous and limited slewing systems differ in more than just the maximum angle. Continuous (360°) systems use a slip-ring or cable-reel arrangement to carry power and control signals across an unlimited number of rotations in either direction, which adds cost and a maintenance item but removes any need to "unwind" the crane. Limited-slewing systems can route cables directly, since the boom never completes a full turn, which simplifies the electrical design but requires the operator or control system to respect the mechanical or electronic stop points at all times.

    How the Slewing Mechanism Works

    Four components work together to deliver controlled rotation, and each has its own role in both performance and long-term reliability:

    • Slewing bearing: a large-diameter rolling-element bearing connecting the rotating upper structure to the fixed portal frame. It carries the full vertical load of the boom and hoisted cargo, plus the overturning moment created whenever the boom is extended out from center. Because it takes both radial and axial loads simultaneously, the slewing bearing is one of the highest-stress components on the entire crane and is usually the first place inspectors look during periodic structural surveys.
    • Slewing drive: electric or hydraulic motors, geared down through a pinion and large ring gear, that rotate the upper structure at a controlled, adjustable speed. Multiple drive units are often used in parallel on larger cranes to distribute torque evenly around the ring gear and avoid uneven wear on one side of the gear teeth.
    • Boom movement (luffing): raises or lowers the boom to change working radius independently of rotation, using either a wire-rope luffing system or hydraulic cylinders depending on the crane's size and duty class.
    • Coordinated lifting and rotation: modern PLC-based control systems let hoisting, luffing, slewing, and rail travel run simultaneously rather than one motion at a time. This is what actually shortens cycle times in practice , a crane with a wide slewing range but a control system that only permits one motion at a time will still be slower than a modest-range crane with fully coordinated motion control.

    Why Does Slewing Range Matter in Dock Operations?

    Improving Cargo Handling Efficiency

    A wider slewing range lets one crane transfer cargo directly between the ship's hold and shore-side receiving points , conveyors, stockpiles, trucks, or rail cars , without repositioning along the quay for each cycle. This matters most on repetitive-cycle work like bulk discharge, where the crane may complete a pick-swing-drop-return cycle every 60–90 seconds; even small reductions in wasted travel compound quickly across a full shift.

    Maximizing Working Coverage

    Combined with rail travel and boom luffing, slewing range extends a crane's effective footprint well beyond the area directly beneath it, letting a single unit serve a long stretch of berth from a small number of fixed rail positions. In practice, port planners often model the "coverage envelope" of each crane position as an arc-and-radius footprint, then space rail stopping points so envelopes overlap slightly , full slewing range reduces the number of stopping points needed to cover a given quay length.

    Reducing Vessel Turnaround Time

    Every repositioning move , braking, traveling, re-aligning , adds non-productive time to a lift cycle. A slewing range matched to the actual pick-and-place geometry of a berth reduces the number of these moves per shift, and because vessel turnaround time directly affects port fees, berth scheduling, and vessel operating costs, even a modest reduction in repositioning frequency can have a measurable commercial impact over a full port call.

    Enhancing Operational Safety

    Slewing systems are paired with rotary limit switches that track angular position and automatically stop rotation at a preset boundary, preventing the boom from over-rotating into adjacent structures, other cranes, or restricted zones. These switches are especially important where multiple cranes operate close together or near fixed structures, since they play a direct role in collision avoidance and site coordination. On busy multi-crane berths, slewing limit devices are frequently combined with radar, laser, or camera-based anti-collision systems that detect other cranes or obstacles and issue warnings or automatically stop the crane before contact occurs. Together, these systems mean that a wider slewing range does not have to come at the cost of reduced safety, provided the limit and detection systems are specified and commissioned correctly.

    Minimizing Equipment Repositioning

    Henan Mine Crane manufactured crane that can reach both the vessel and the storage or transfer point from one slewing arc removes the need to reposition along the rail between nearly every lift , a meaningful driver of daily lift-cycle counts on high-volume berths. Fewer repositioning moves also mean less wear on the travel drive and rail wheels, which can extend maintenance intervals on that part of the crane even as slewing-system wear increases slightly with higher rotational duty.

    Factors That Determine the Ideal Slewing Range

    Dock Layout and Available Space

    Berths with tight clearances to adjacent cranes, buildings, or overhead structures may need a restricted slewing arc, or a slewing range paired with software-defined "no-go" zones, rather than unrestricted 360° rotation. Older ports retrofitted with newer cranes often face this constraint directly, since the original quay layout was rarely designed with full-circle crane rotation in mind, and moving fixed structures to accommodate a new crane is usually far more expensive than specifying a restricted slewing angle from the start.

    Vessel Size and Berthing Position

    Larger vessels with a wide beam and multiple hatch positions generally benefit from full rotation, since the crane needs to reach across the entire vessel width as well as swing back to the shore side. Terminals that serve a mix of vessel sizes , from small coasters to larger bulk carriers , also tend to favor full slewing, since a fixed berthing position that works well for one vessel class may put a different vessel's hatches at an angle that a restricted-arc crane cannot reach without moving.

    Cargo Type

    • Bulk cargo(coal, ore, grain) : favors continuous slewing paired with grab attachments for high-throughput, repetitive-cycle discharge, since the crane is typically swinging between the same two or three points hundreds of times per shift and any restriction on the arc directly limits achievable tonnage per hour.
    • General cargo: benefits from full rotation combined with precise hook control for placement accuracy, particularly when handling steel coils, machinery, or palletized goods that need to be set down in a specific orientation rather than simply released.
    • Heavy project cargo: priority is a stable working radius and load chart at the required angle over slewing speed, since project cargo lifts are typically slower, more deliberate operations where positioning accuracy matters more than cycle time.
    • Containers: slewing flexibility matters less than consistent hook height and spreader alignment, since container terminals typically rely on rail-mounted or ship-to-shore cranes for the highest-volume moves, with portal slewing cranes more often used for smaller berths or as supplementary equipment.

    Lifting Capacity and Boom Length

    Load charts change with radius and slew angle: as boom length and rated capacity increase, the achievable combination of radius and full-circle rotation is constrained more by structural and stability limits than by the drive system itself. A longer boom carrying a heavier rated load creates a larger overturning moment at full radius, which can mean the crane's rated capacity is lower at certain points in the slew arc even on a mechanically unrestricted 360° design , buyers should always check the full load chart across the entire rotation, not just the headline maximum capacity figure.

    Operating Radius Requirements

    The interaction between slewing range and radius determines total working coverage , a crane can have full 360° rotation but still be limited in practical usefulness if its radius doesn't reach both the vessel hold and the shore-side stacking area. Port planners should map both dimensions against the actual dock geometry before finalizing a specification, since a crane specified with generous slewing range but insufficient radius will still require rail repositioning to reach key pick or drop points.

    Number of Cranes Operating Simultaneously

    Where two or more portal cranes share a berth or travel the same rail, slewing ranges are sometimes intentionally restricted on the inboard side, backed by anti-collision sensors, to prevent boom overlap during simultaneous operation. This is a common design compromise on multi-crane quays: rather than relying solely on operator judgment and anti-collision electronics to prevent contact, some terminals build in a mechanical slewing limit as a hard backstop, accepting a small reduction in coverage in exchange for a simpler, more predictable safety envelope.

    Recommended Slewing Ranges for Different Dock Applications

    Bulk Cargo Terminals

    Full or near-full rotation (270°–360°) is standard, since bulk terminals need the crane to swing repeatedly between the vessel hold and shore-side hoppers, conveyors, or open stockpiles at high cycle rates. Terminals handling coal, ore, or grain typically prioritize continuous slewing specifically because throughput is measured in tonnes per hour, and any repositioning between cycles directly reduces that figure.

    General Cargo Ports

    270°–360° slewing supports the mixed handling patterns typical of general cargo , steel coils, machinery, bagged goods, and break-bulk freight moving between varied pick and drop points. Because general cargo terminals rarely have a single repetitive cycle, the flexibility of a wide slewing arc tends to matter more here than raw slewing speed.

    Shipyards

    180°–360° is common. Full rotation supports hull block turning and section transfer around a dry dock from a single rail position, letting the crane reach every point around the dock without repositioning, which cuts crane movement time during assembly. Where the crane works close to fixed shore structures , outfitting halls, cable gantries, or adjacent slipways , a restricted arc paired with limit switches is used instead, since shipyard layouts are often denser and more permanent than open bulk terminal yards.

    Offshore Engineering Bases

    360° is typically specified, since offshore fabrication and load-out work requires maximum positional flexibility around large, irregular components such as jacket structures, modules, and topside equipment that cannot always be approached from a predictable angle.

    Multi-Purpose Ports

    360° slewing supports the widest range of cargo types , bulk, general, and project cargo , on the same crane without reconfiguration between shifts, which is particularly valuable for smaller or mid-sized ports that cannot justify dedicated single-purpose cranes for each cargo stream.

    Slewing Range by Dock Application

    ApplicationMain Advantage
    Bulk Cargo TerminalWide cargo coverage, high-cycle discharge
    General Cargo PortFlexible handling of mixed cargo types
    ShipyardPrecise component positioning around dry dock
    Offshore BaseMaximum operational flexibility
    Multi-Purpose PortHandles multiple cargo types efficiently

    270° vs. 360° Slewing: Which One Is Better?

    Advantages of 270° Slewing

    A restricted arc reduces the risk of boom interference with adjacent structures, other cranes, or overhead cable routing, and can simplify the design of trailing cable or hose management systems since the Henan Mine Crane manufactured crane never has to complete a full rotation. It can also reduce upfront cost slightly, since the electrical system does not need slip rings or a cable-reel assembly rated for continuous rotation, and it gives site planners a simpler, more predictable safety envelope to design around when other fixed infrastructure sits close to the crane.

    Advantages of 360° Continuous Slewing

    Unrestricted rotation lets a single crane position serve the full working arc , both vessel and land side , without ever needing to reposition, which is the main reason full slewing is the default specification for most dock portal cranes. It also gives operators more flexibility to approach a load from whatever angle is most convenient, rather than always having to work within a fixed sector, which can reduce operator fatigue and improve placement accuracy over a long shift.

    Limitations of Each Design

    270° designs limit coverage on the restricted side and can force additional rail travel to reach positions outside the arc, which partially offsets the cost savings if the terminal's cargo flow regularly requires reaching both sides of the crane. 360° designs require more robust cable management (slip rings or cable reels) and typically depend more heavily on limit switches and anti-collision systems when working in close proximity to other equipment, adding a recurring maintenance and calibration requirement that a restricted-arc crane avoids.

    Which Option Delivers Better Productivity?

    For most dock applications , bulk, general cargo, and multi-purpose berths , 360° slewing delivers higher productivity because it removes repositioning almost entirely. 270° is the better choice specifically where site geometry, adjacent cranes, or fixed structures make full rotation impractical or unsafe, not as a general-purpose alternative.

    How Slewing Range Affects Crane Performance

    Operating Efficiency

    Wider slewing range generally shortens average cycle time by reducing the number of rail repositioning moves per shift, provided the drive system and control logic support smooth, simultaneous slew-and-luff motion.

    Load Stability

    Rated capacity typically decreases as working radius increases, regardless of slew angle , the load chart, not the slewing range itself, is what governs safe lifting at any given position. Stability is also affected by wind loading on the boom and load, which is why dock cranes typically carry reduced capacity ratings, or operating restrictions, above certain wind speed thresholds regardless of which direction the boom is slewed.

    Positioning Accuracy

    Fine positioning near the end of a slew movement , bringing a load gently into its final position over a stockpile or vessel hatch , depends on the drive's ability to decelerate smoothly, a control-system characteristic that is independent of the crane's maximum slewing angle.

    Maintenance Requirements

    The slewing bearing and ring gear are subject to continuous wear proportional to total rotational cycles, so higher-utilization full-slewing cranes generally need closer inspection intervals for the bearing and drive train than limited-arc units doing the same duty cycle.

    Energy Consumption

    Continuous slewing at high duty cycles draws more cumulative energy than a restricted arc doing an equivalent number of lifts, though the difference is generally small relative to hoisting energy demand on most dock cranes. For terminals tracking energy costs closely, the marginal difference in slewing energy use is rarely the deciding factor in choosing between 270° and 360° , hoisting speed, duty cycle, and cargo weight typically account for a much larger share of total energy consumption.

    How to Select the Right Portal Slewing Crane for Your Dock

    Evaluate Port Throughput

    Match slewing range and speed to your target lifts-per-hour figure , a high-throughput bulk terminal justifies the extra cost of full continuous slewing more readily than a low-volume, occasional-use berth. Modeling expected cycle times against actual dock geometry before finalizing a specification helps avoid over- or under-specifying the crane relative to real operational demand.

    Match the Crane to Cargo Types

    Confirm slewing range against your actual cargo mix (bulk, general, project, or container) rather than defaulting to the maximum available spec. If cargo mix is expected to change over the crane's service life, it's worth discussing with the manufacturer whether the base design can accommodate a future range or capacity upgrade.

    Consider Future Expansion Plans

    Specifying 360° slewing even where current operations don't strictly require it can preserve flexibility if the berth's cargo mix or layout changes later, since retrofitting a limited-arc crane for full rotation is a major structural and control-system change involving new slewing bearings, cable management, and control logic rather than a simple adjustment.

    Check Safety and International Standards

    Confirm the crane's duty classification, slewing limit switches, and , where applicable , anti-collision systems meet the relevant structural and safety standards for your region and site conditions. Duty classification in particular should reflect actual expected usage rather than a generic default, since a crane under-rated for its real duty cycle will show premature wear in the slewing bearing and drive components well before its expected service life.

    Choose an Experienced Crane Manufacturer

    Slewing range, boom configuration, lifting capacity, and control systems all need to be engineered together for your specific dock geometry , work with a manufacturer that will model your actual berth layout rather than quoting a standard catalog configuration. A manufacturer familiar with port and shipyard applications can also advise on classification society requirements, spare parts availability, and long-term maintenance planning specific to your slewing system design.

    Frequently Asked Questions (FAQ)

    Q: Is a 360° slewing crane always the best choice?

    No. 360° is the right default for most bulk, general cargo, and multi-purpose berths because it removes repositioning. But in tight, multi-crane berths or sites with fixed overhead structures nearby, a restricted 180°–270° arc paired with limit switches can be the safer and more practical choice.

    Q: What is the standard slewing angle for a portal slewing crane?

    Restricted ranges are specified as exceptions for site-specific space or safety constraints, not as the default.

    Q: Does a larger slewing range improve productivity?

    Generally yes, because it reduces rail repositioning between lifts. But productivity also depends on slewing speed, control system responsiveness, and how well slewing range is matched to the actual cargo flow , a wider arc with a slow drive won't outperform a well-specified narrower one.

    Q: How does slewing range affect maintenance costs?

    Manufacturers can configure slewing range, along with lifting capacity, boom length, and control systems, to match a specific dock layout, and can adjust limit switch settings to define a restricted operating arc even on a mechanically full-rotation crane.

    Henan Mine Crane

    The right slewing range is determined by the unique requirements of each dock rather than a one-size-fits-all specification. Factors such as berth layout, vessel dimensions, cargo types, operating frequency, and future expansion plans should all be evaluated together to ensure the crane delivers the best balance of productivity, safety, and long-term operating efficiency.

    As a professional manufacturer of heavy-duty lifting equipment, Henan Mine Crane Factory provides customized portal slewing cranes engineered for the specific needs of ports, shipyards, and bulk cargo terminals. From slewing range and boom configuration to lifting capacity, intelligent control systems, and complete project support, our engineering team works closely with customers to deliver reliable, high-performance crane solutions that improve operational efficiency, reduce lifecycle costs, and ensure dependable performance in demanding marine environments.

    Discuss the crane arrangement for your project.

    Slewing coverage should follow the vessel position, cargo transfer points and quay obstructions. Show the required working envelope on a site plan and ask the supplier to identify restricted movements and operating limits. Share the load, available drawings, working cycle and site conditions with Henan Mine Crane so the required configuration and supply boundary can be discussed.

    Related crane configurations

    Portal Harbor Crane

    View product parameters
    Lifting capacity: 5t – 400tWorking range: 10m – 50mLifting height: 8m – 40m

    Handle cargo with a portal harbor crane configured for the working radius and lifting appliance. Define hook or grab operation, quay interfaces, outreach and the operating cycle.

    Updated 2026 · Henan Mine Crane
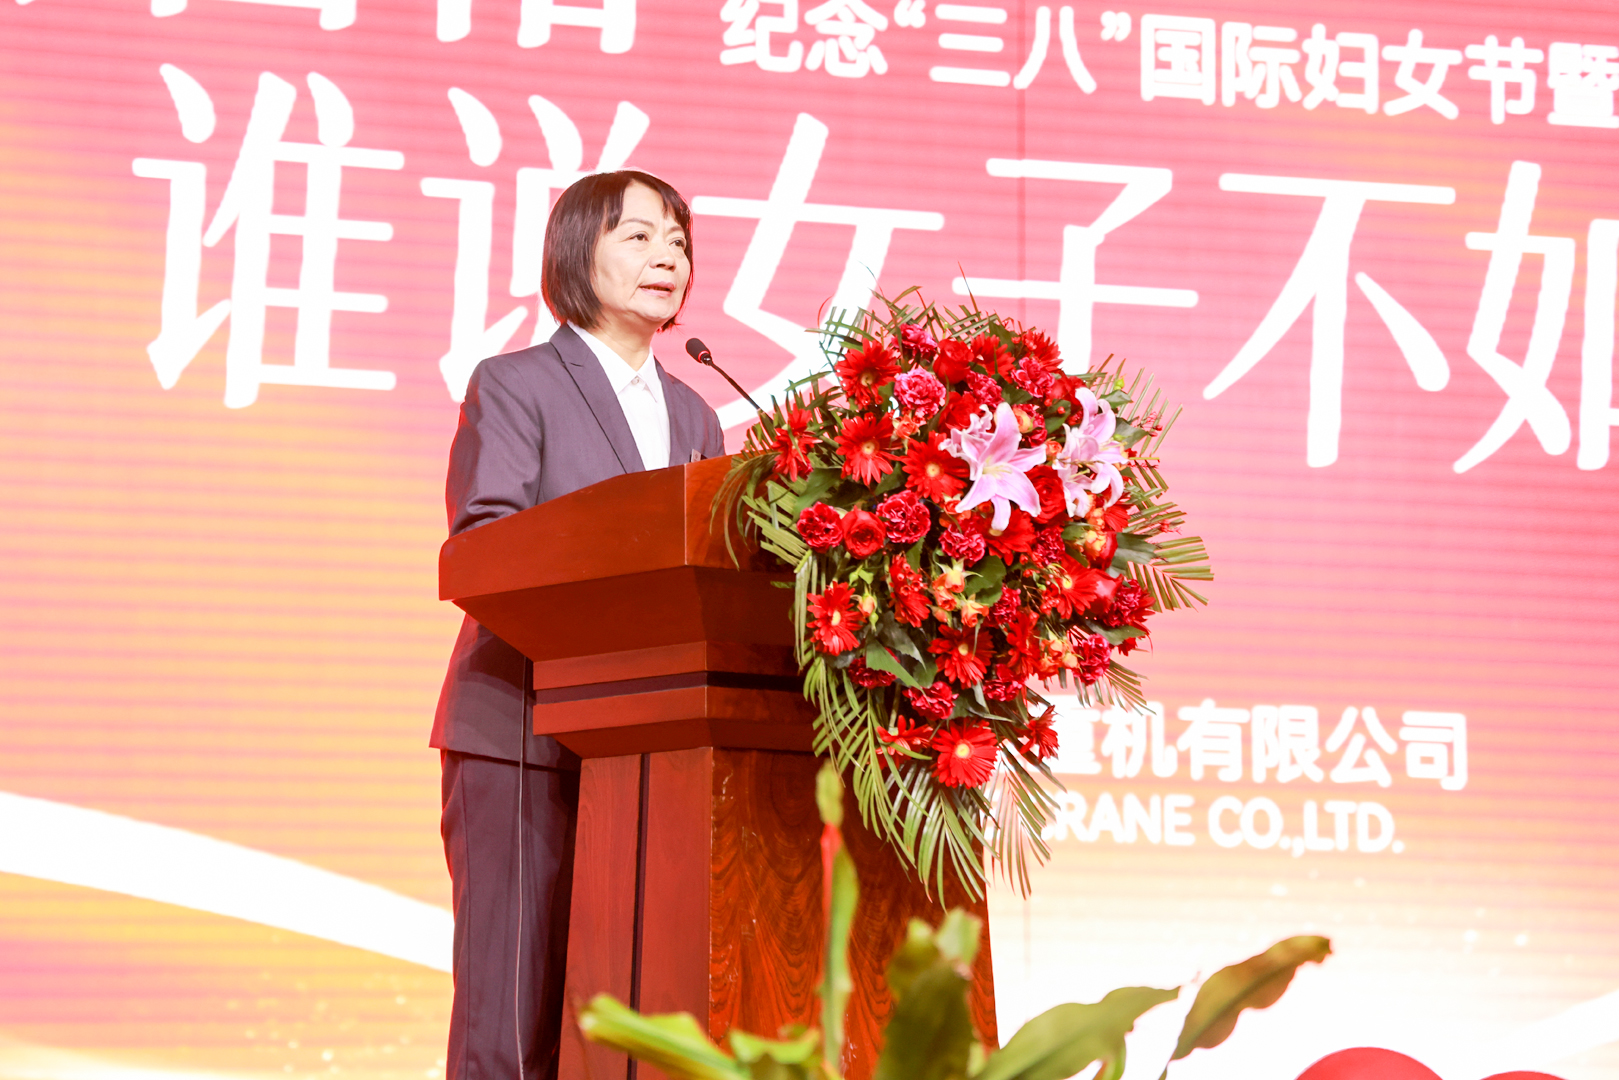
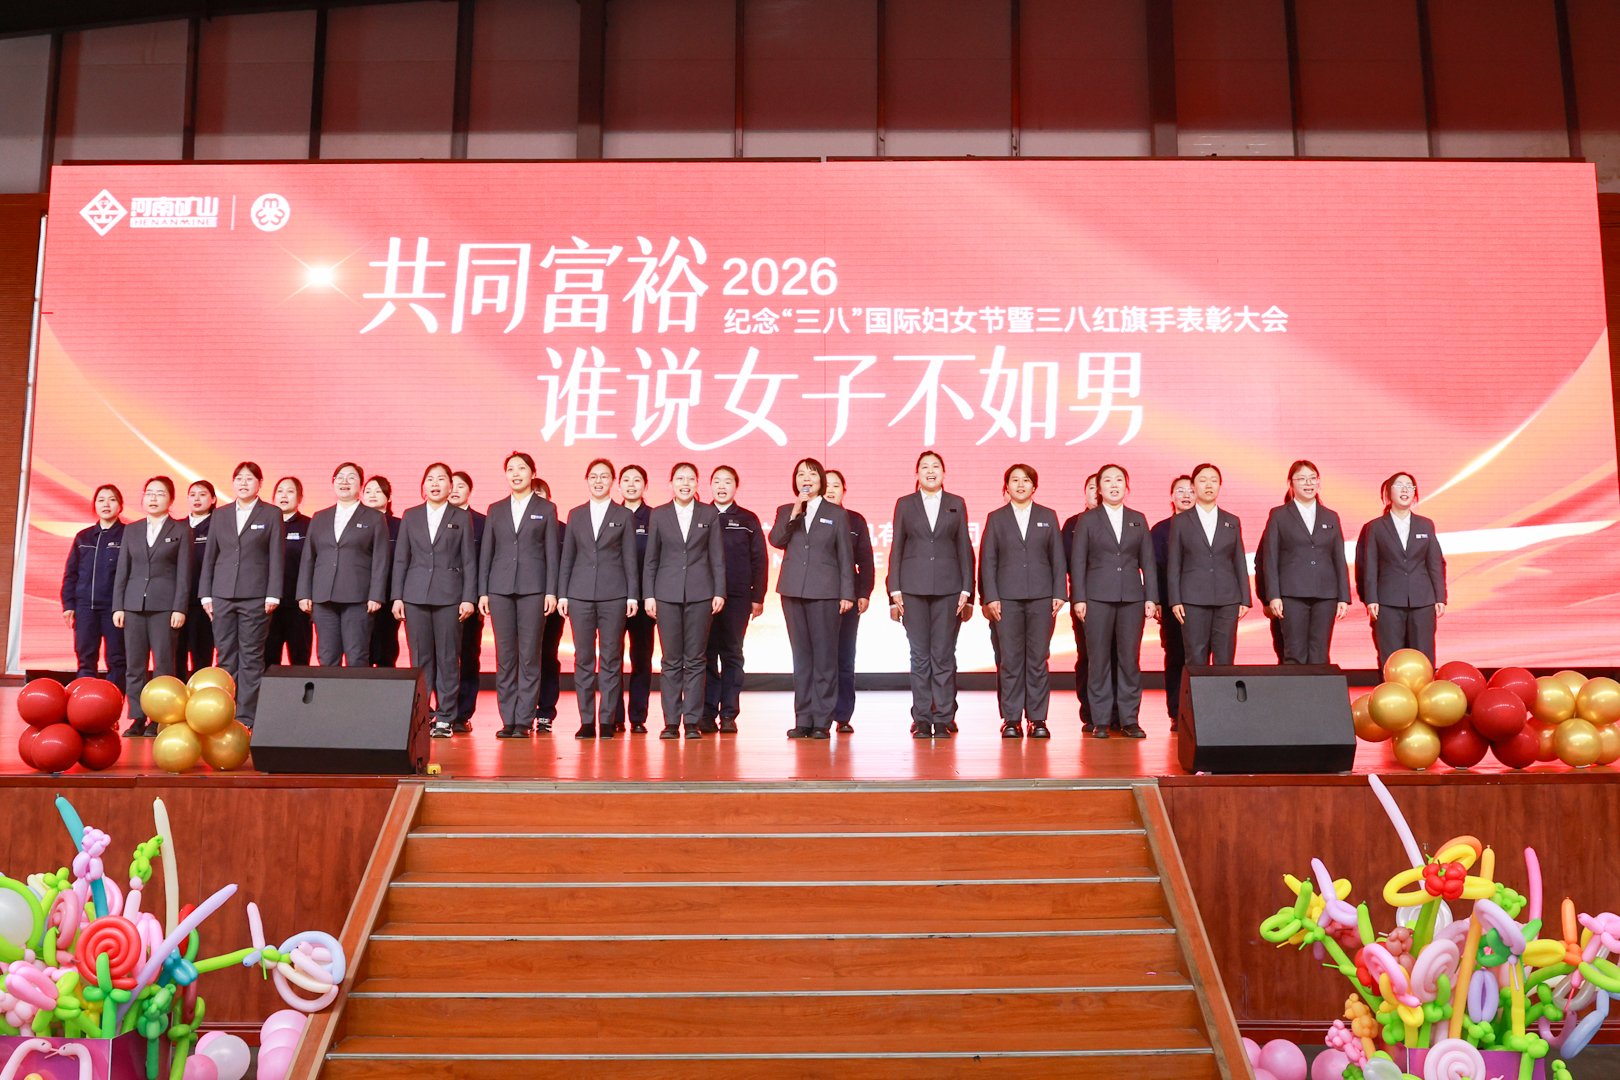
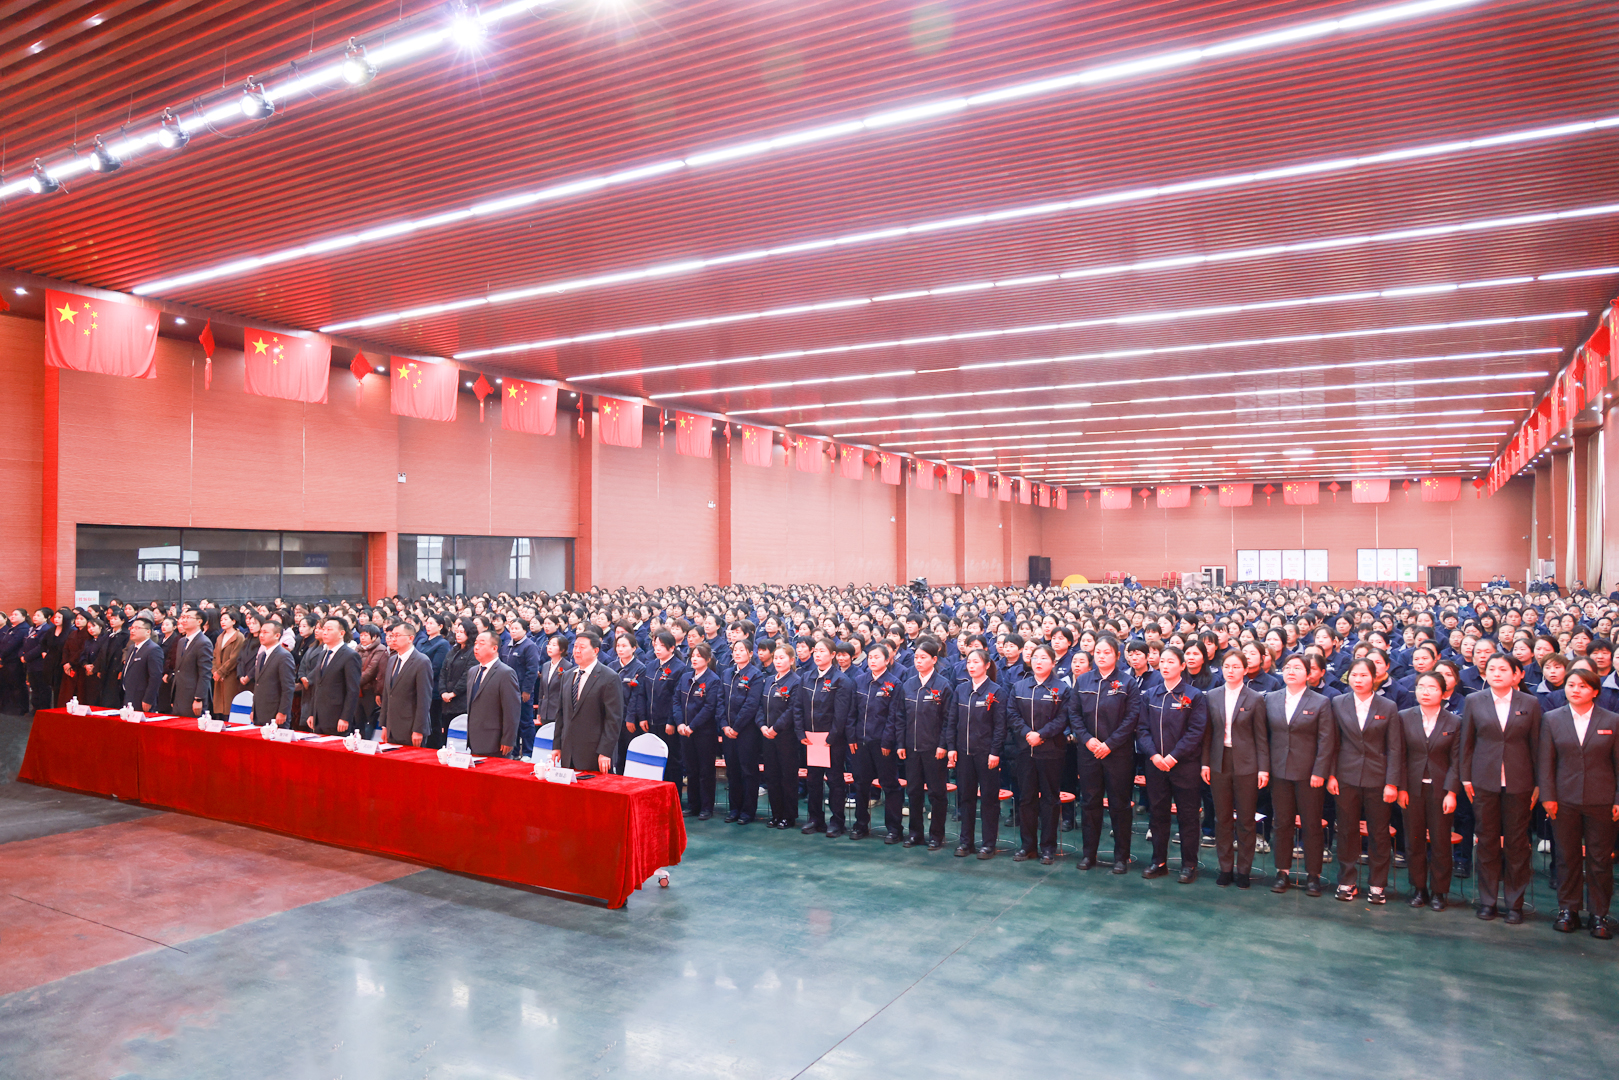
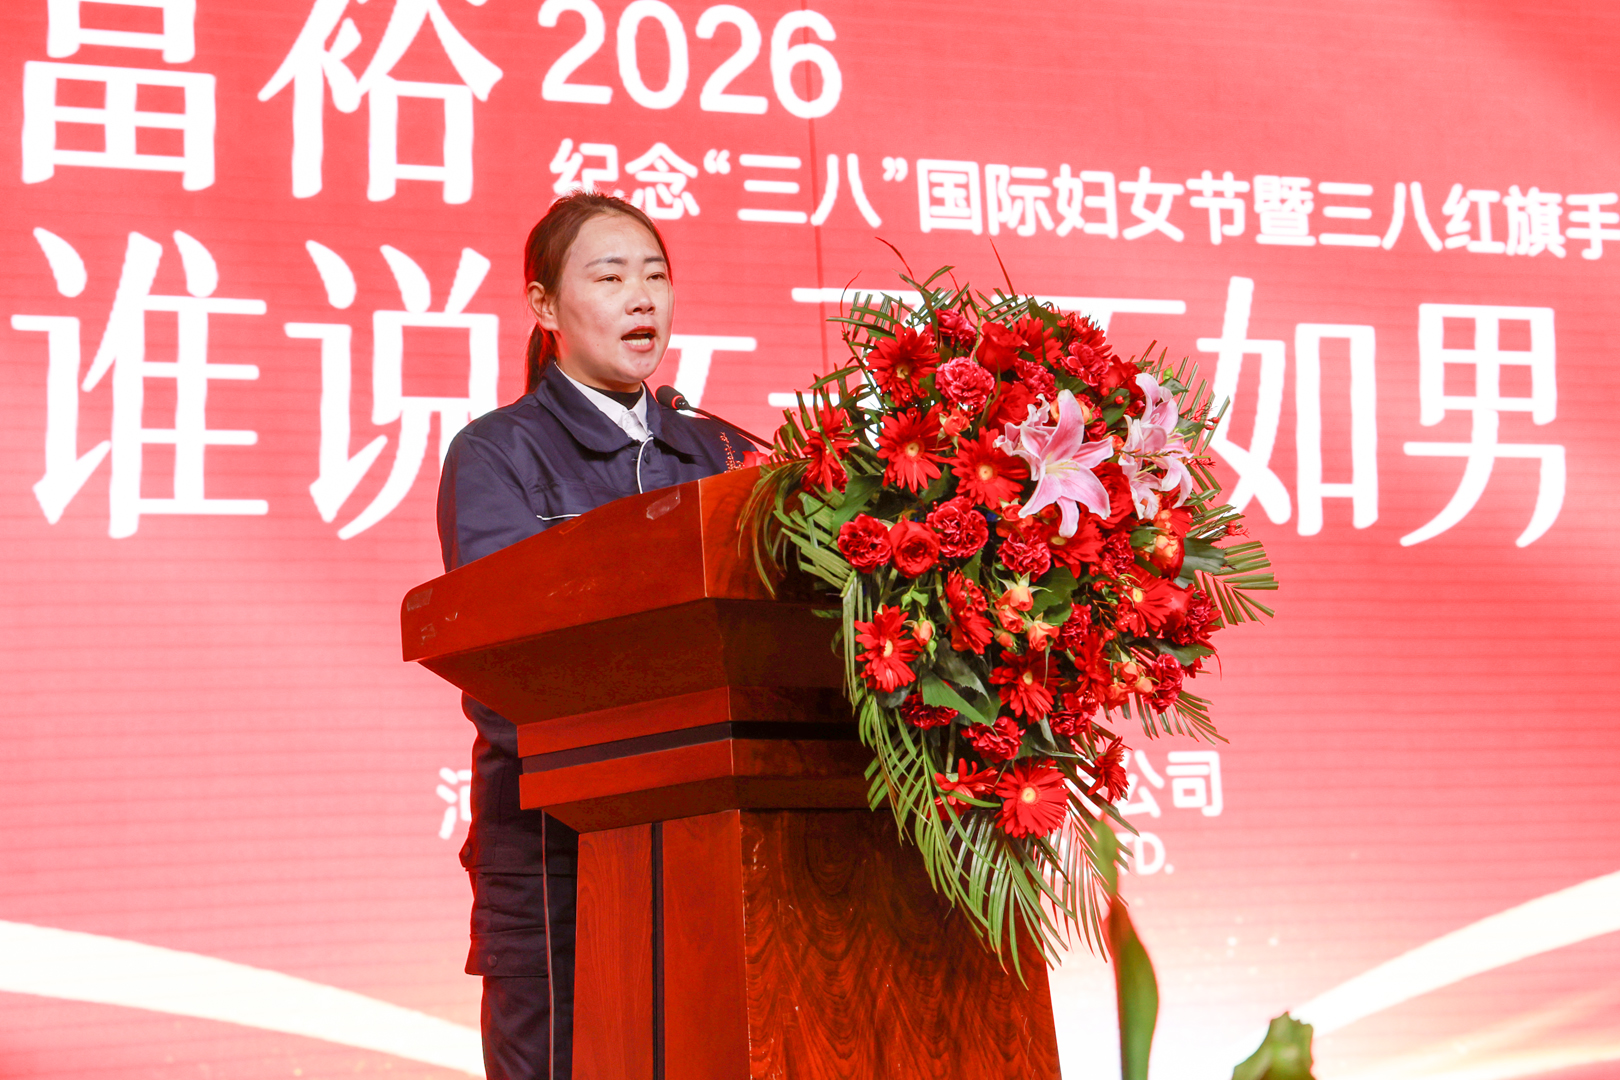
  • Henan Mine Crane Recognises Women Employees Ahead of International Women’s Day

    Henan Mine Crane Recognises Women Employees Ahead of International Women’s Day

    Company & People

    Henan Mine Crane Recognises Women Employees Ahead of International Women’s Day

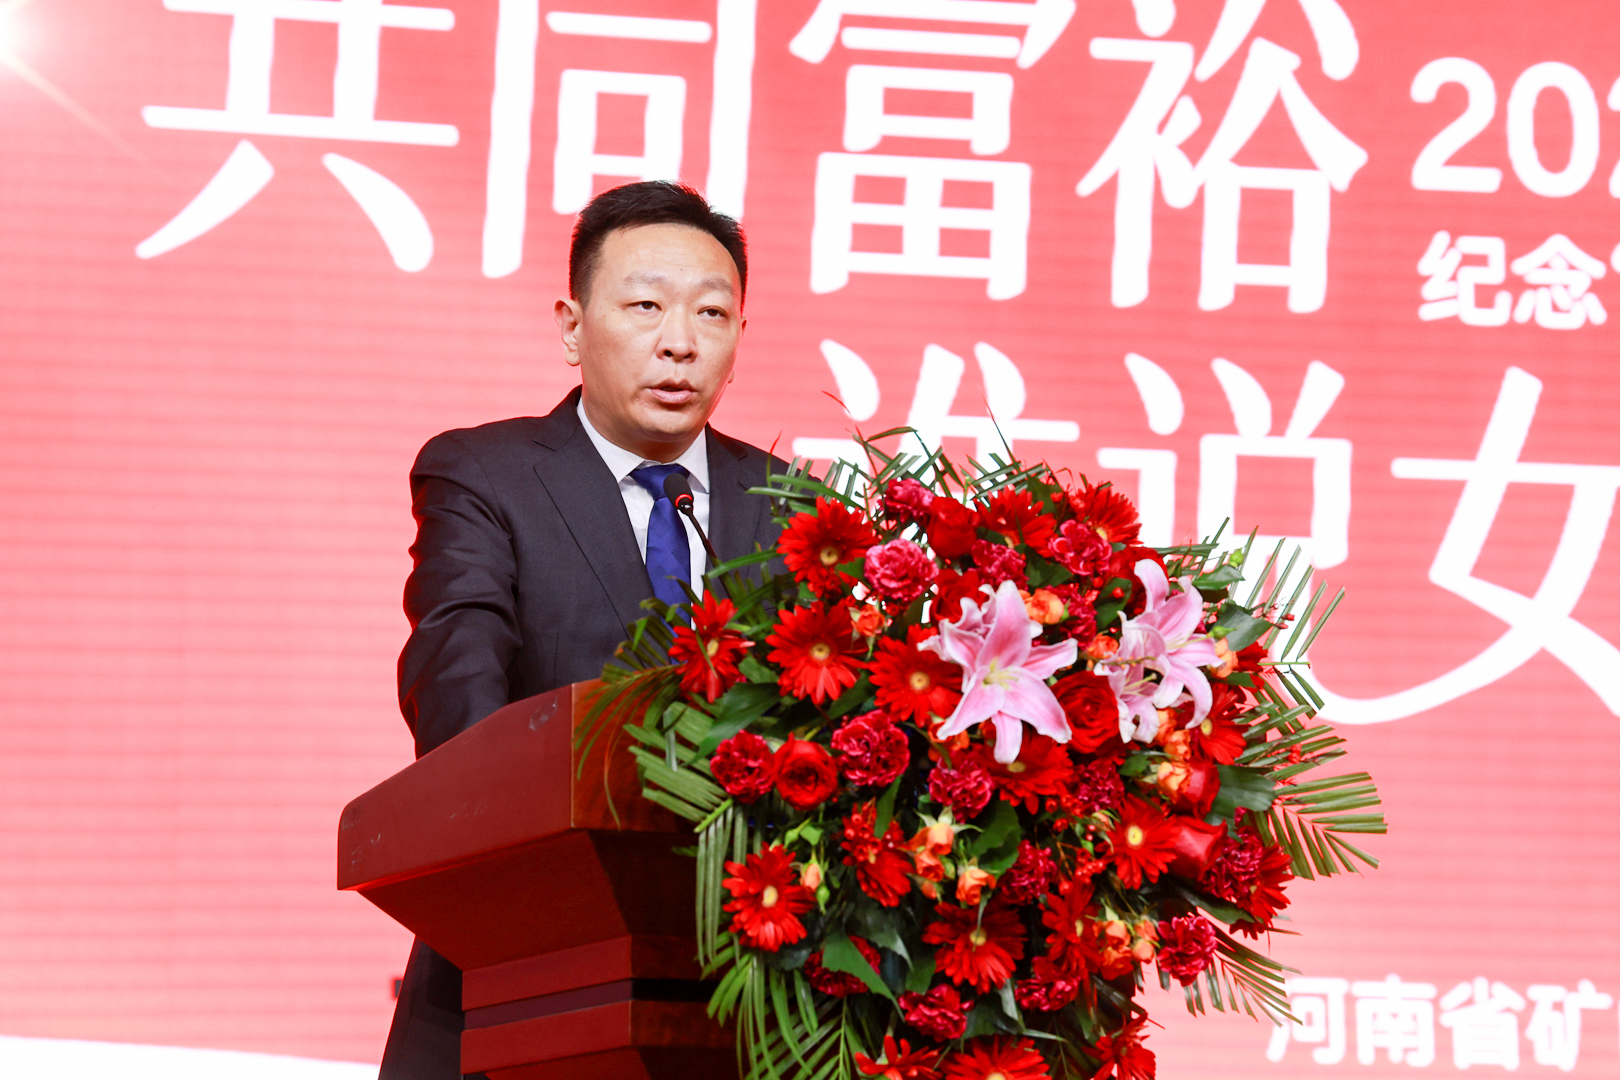
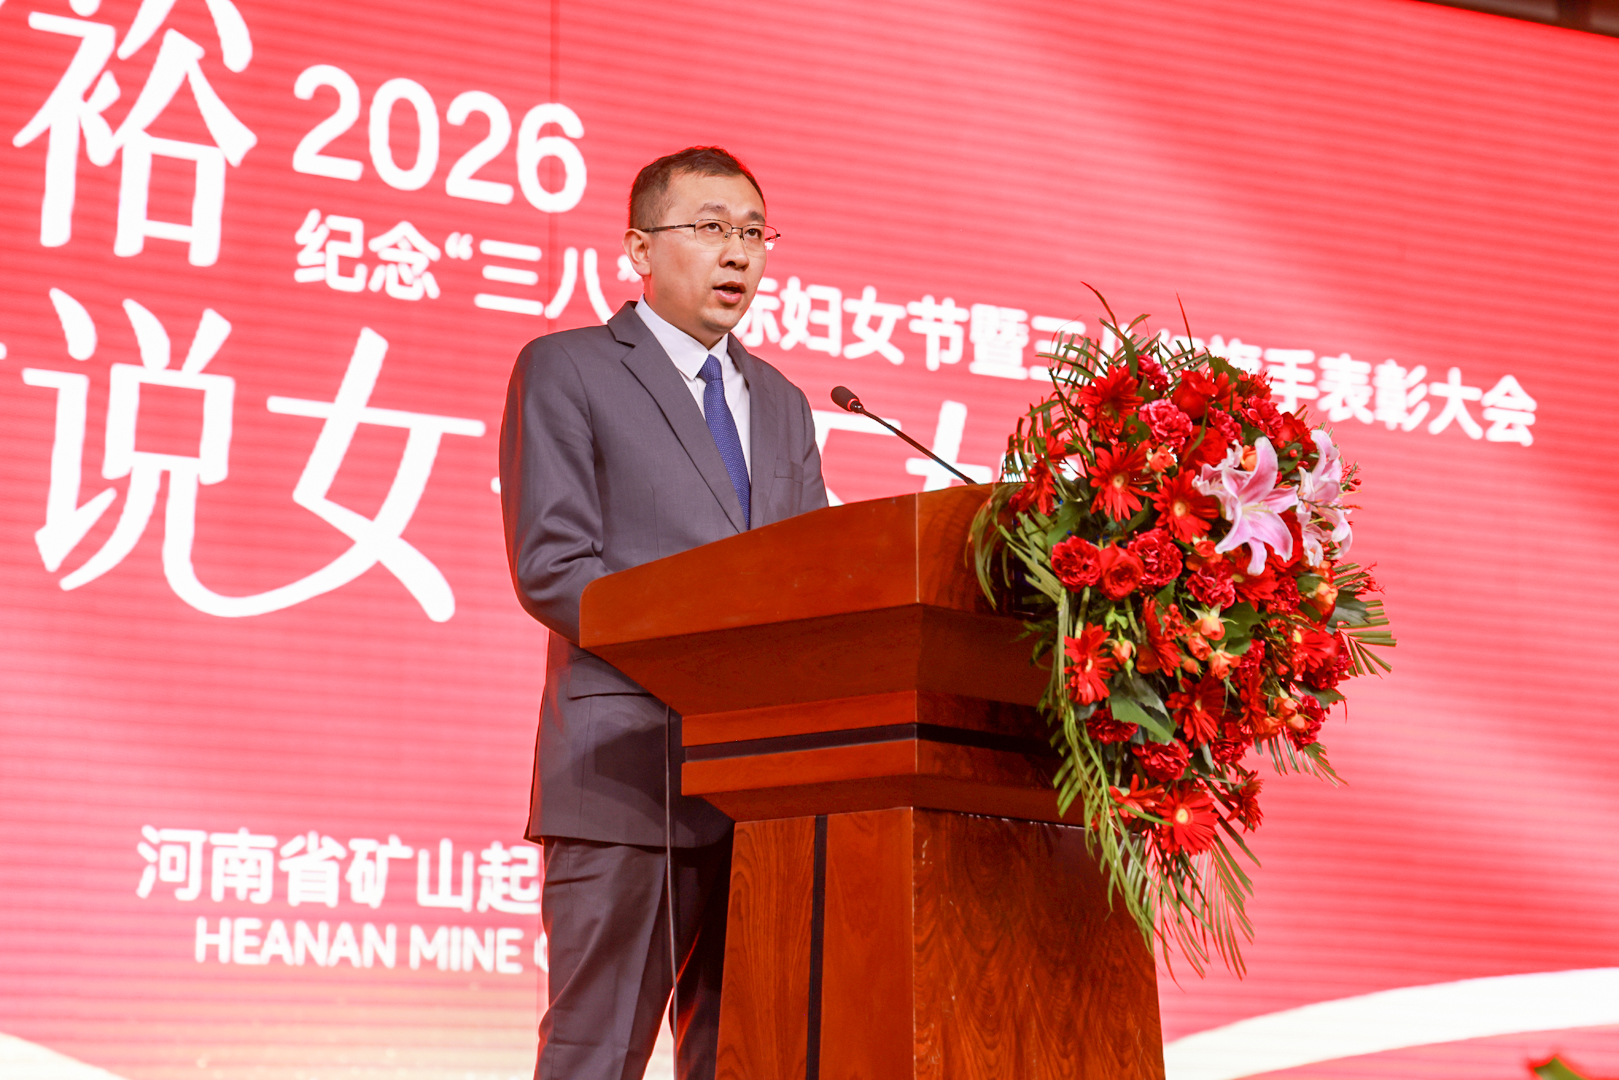
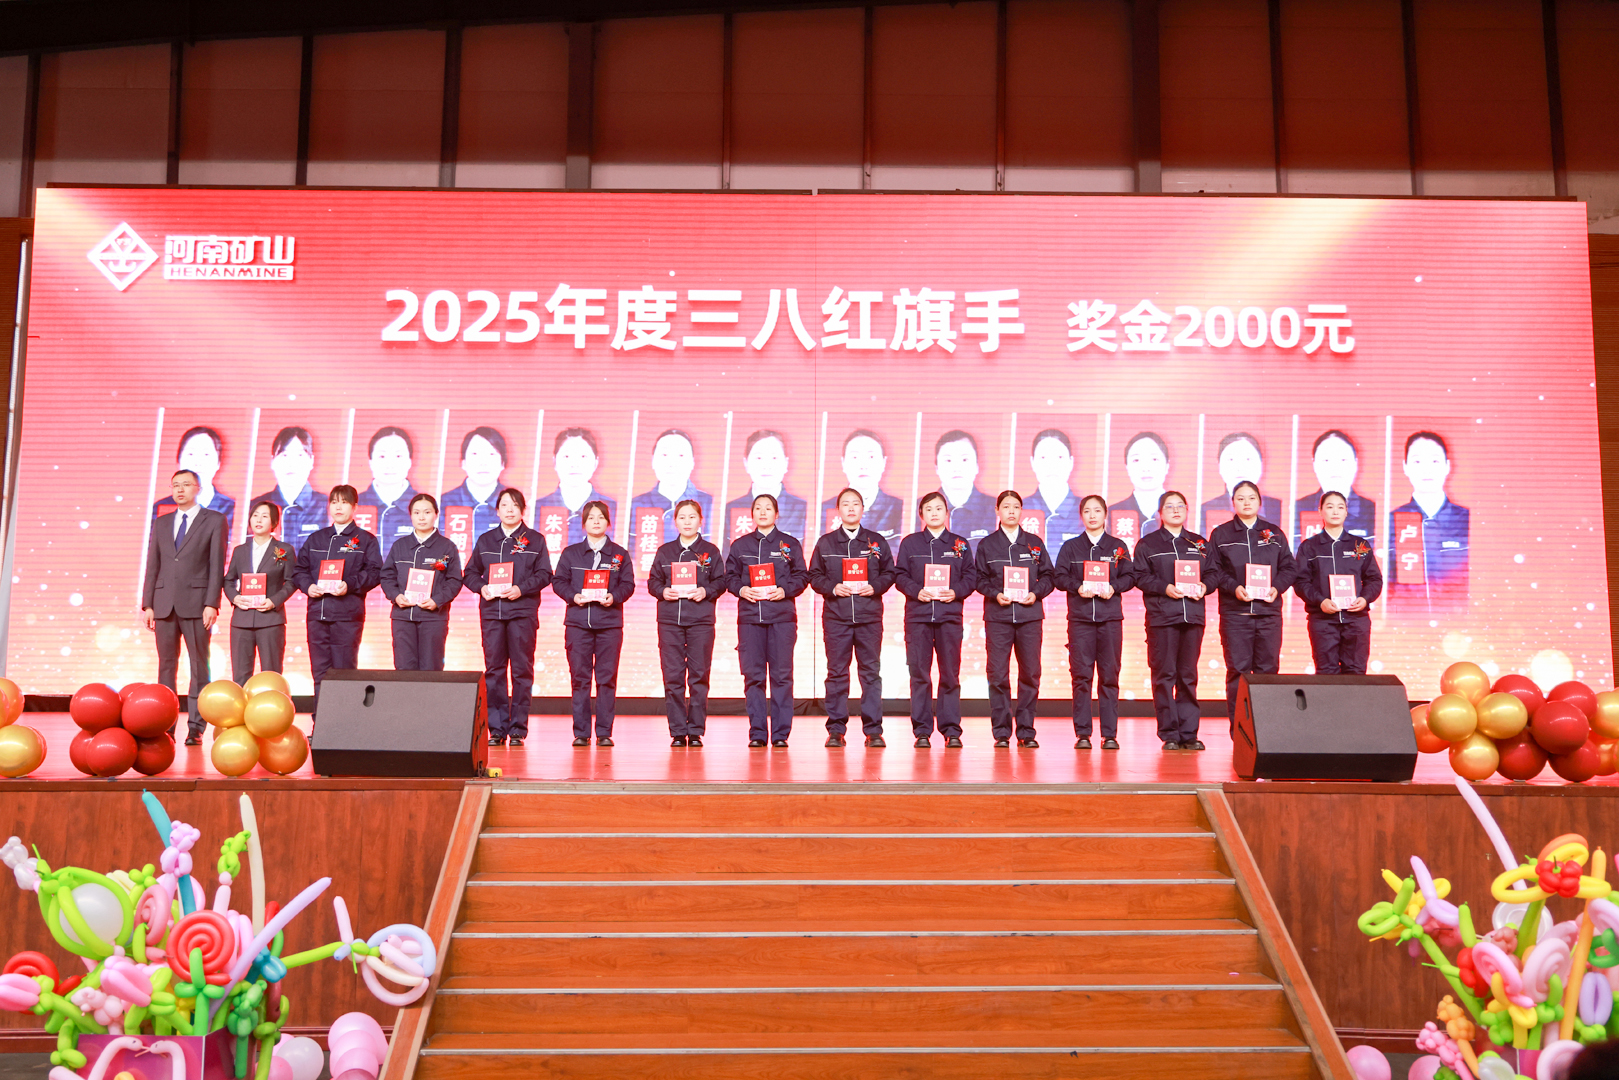
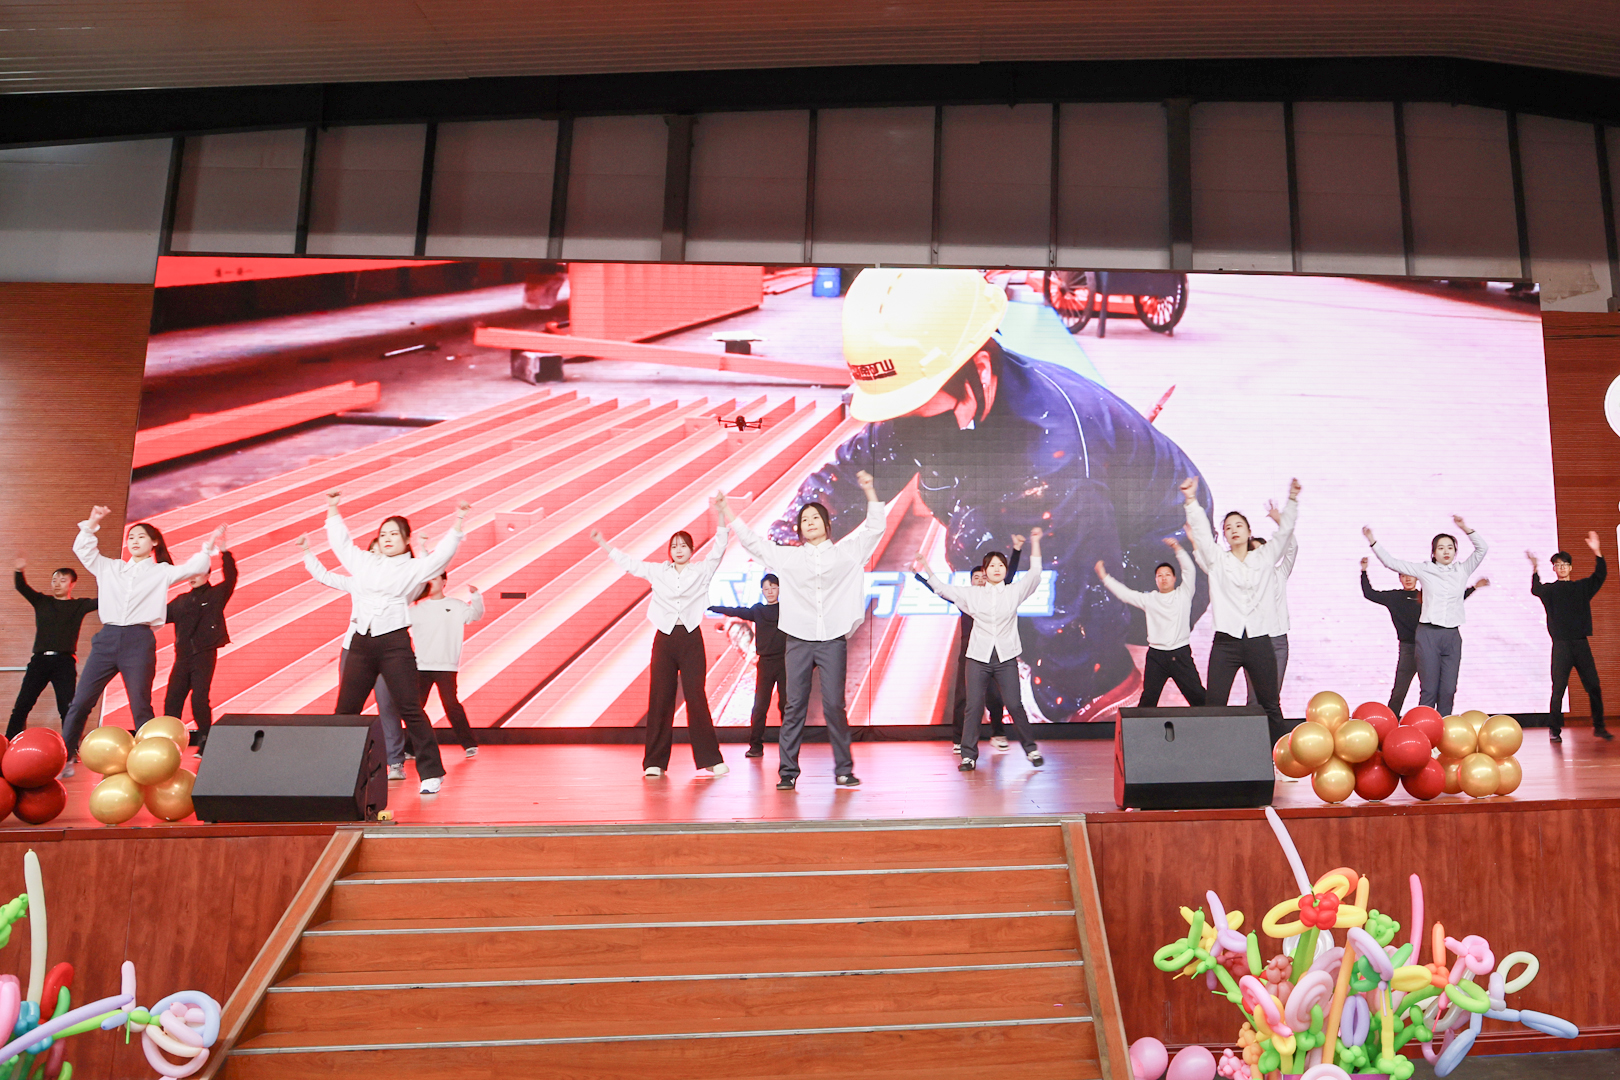
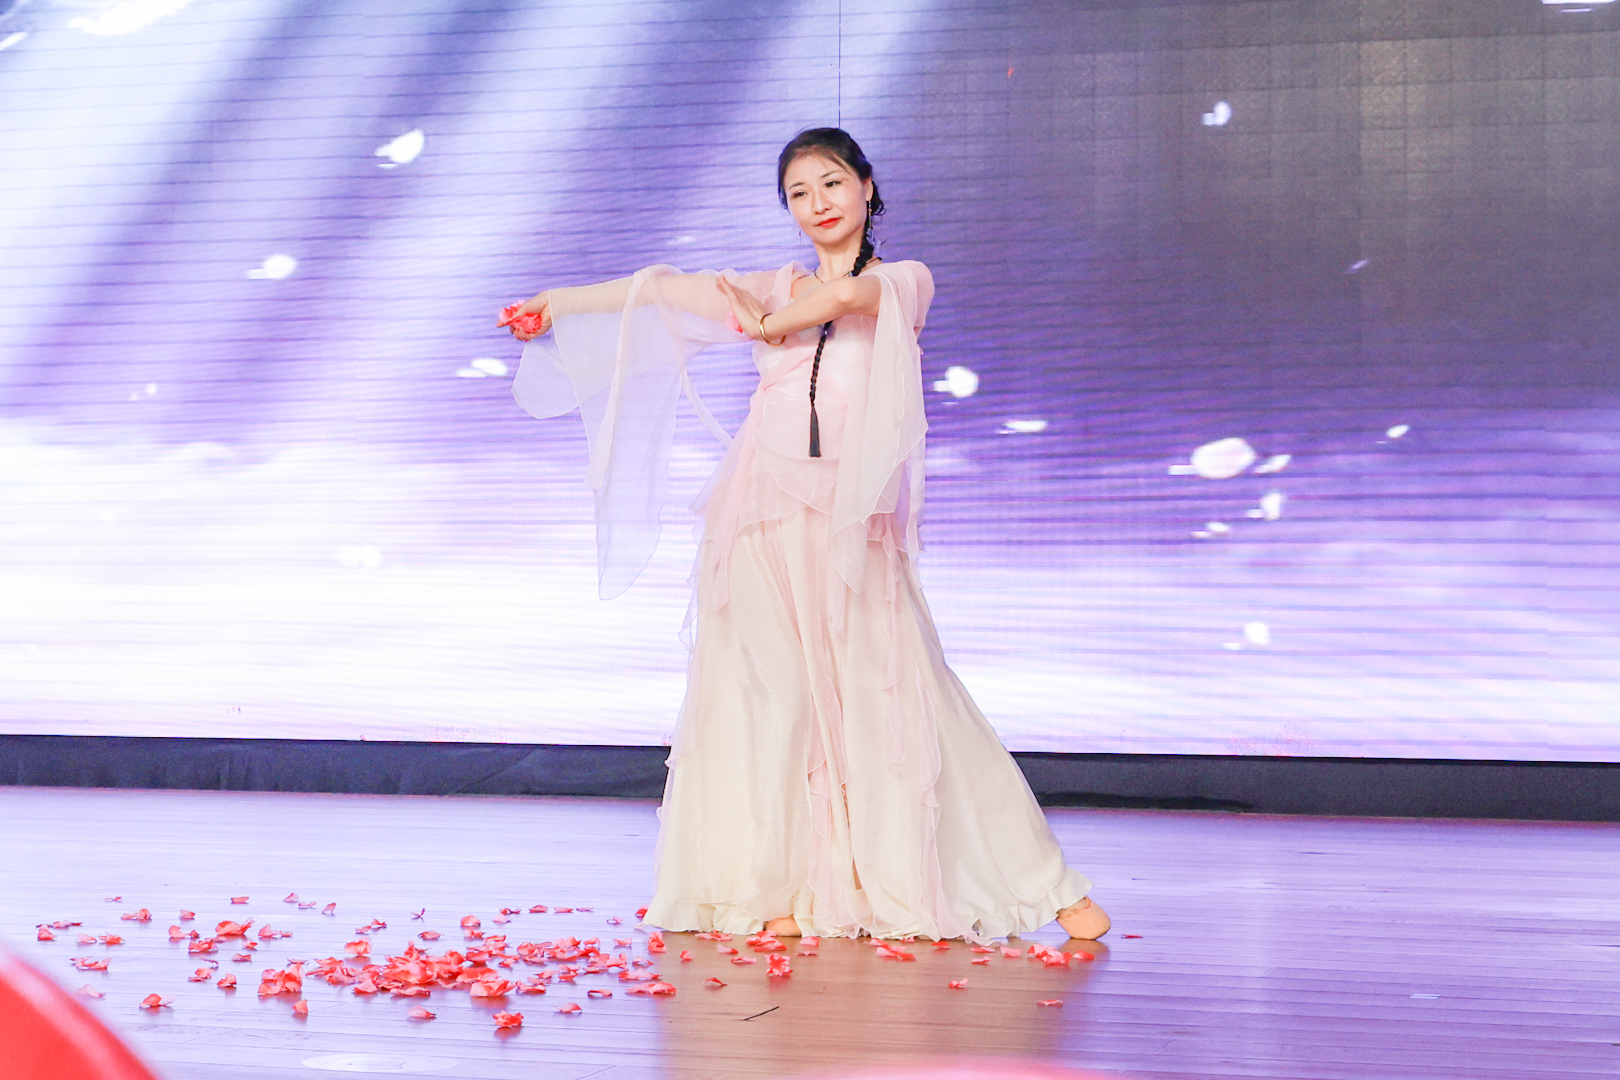
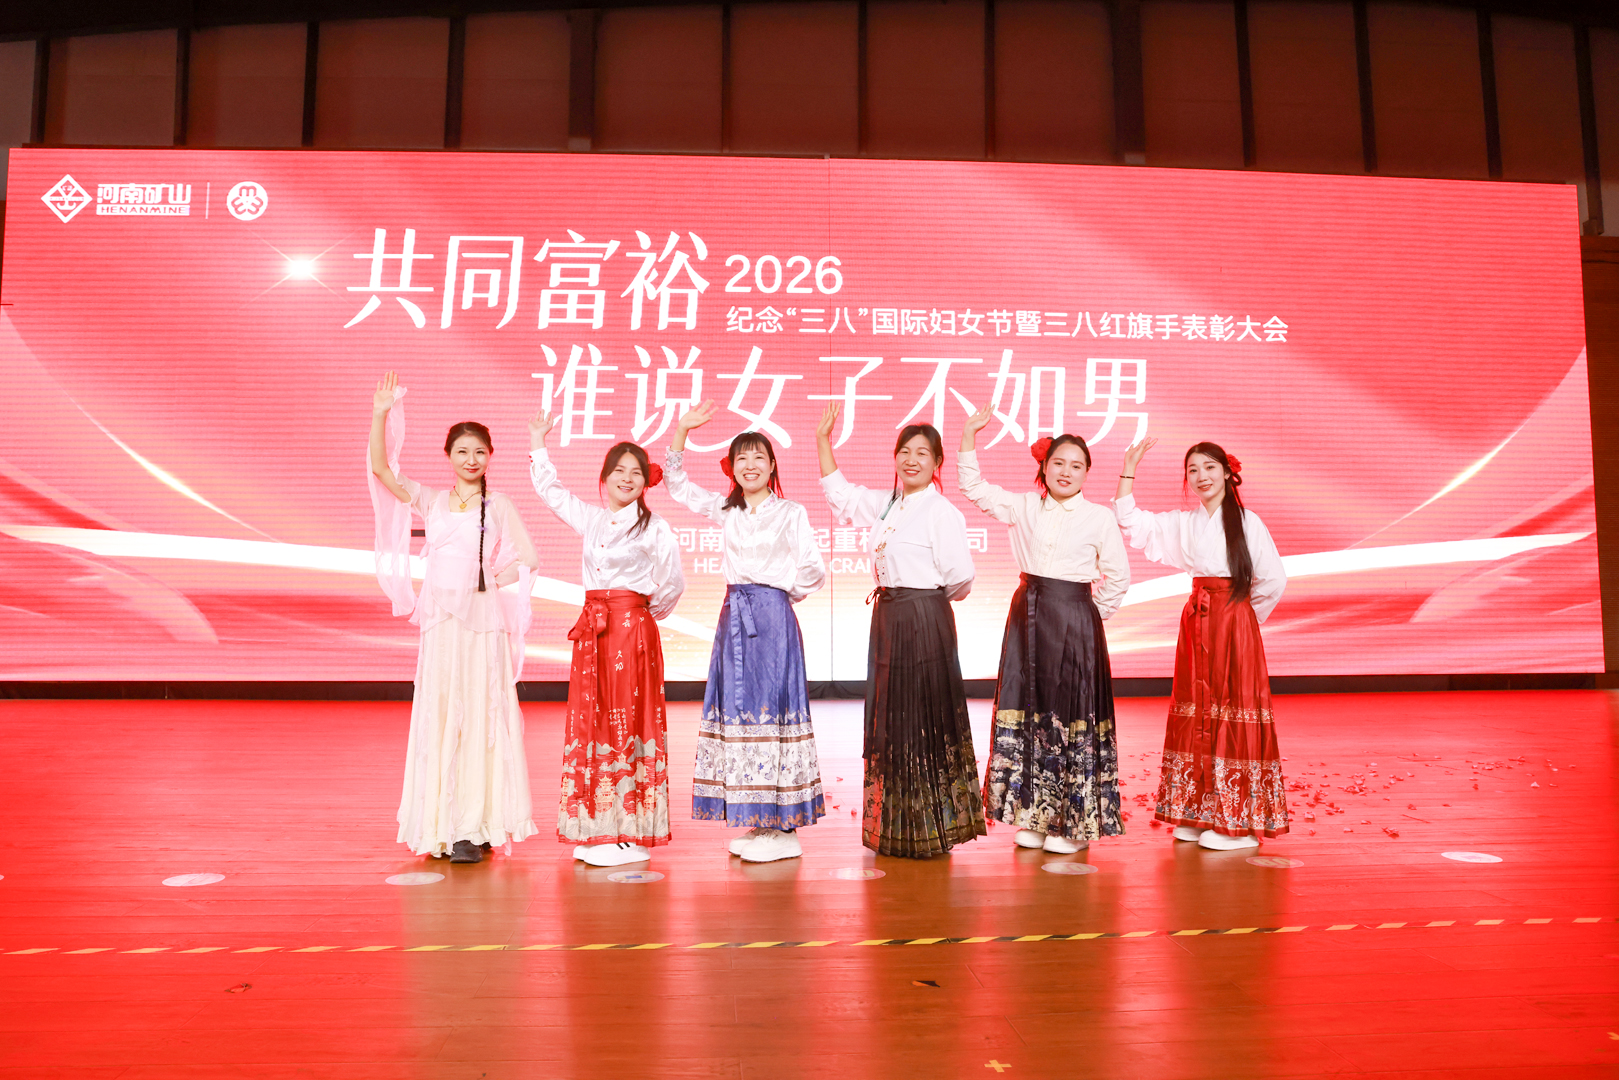
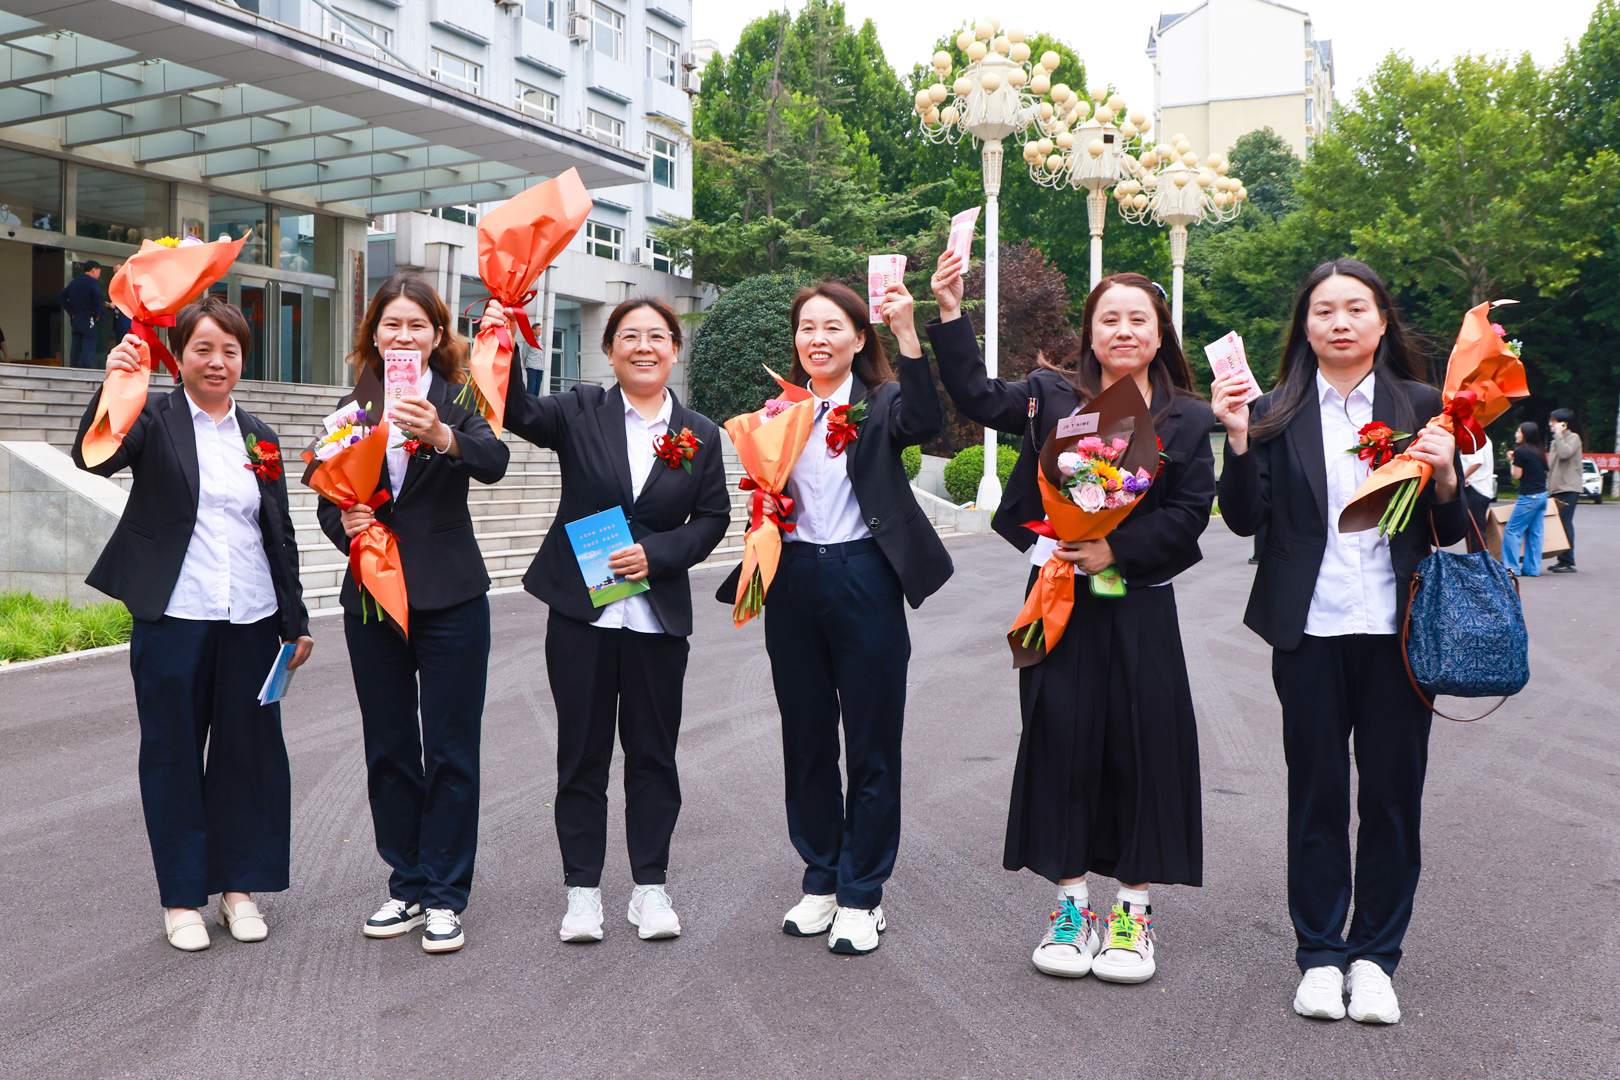
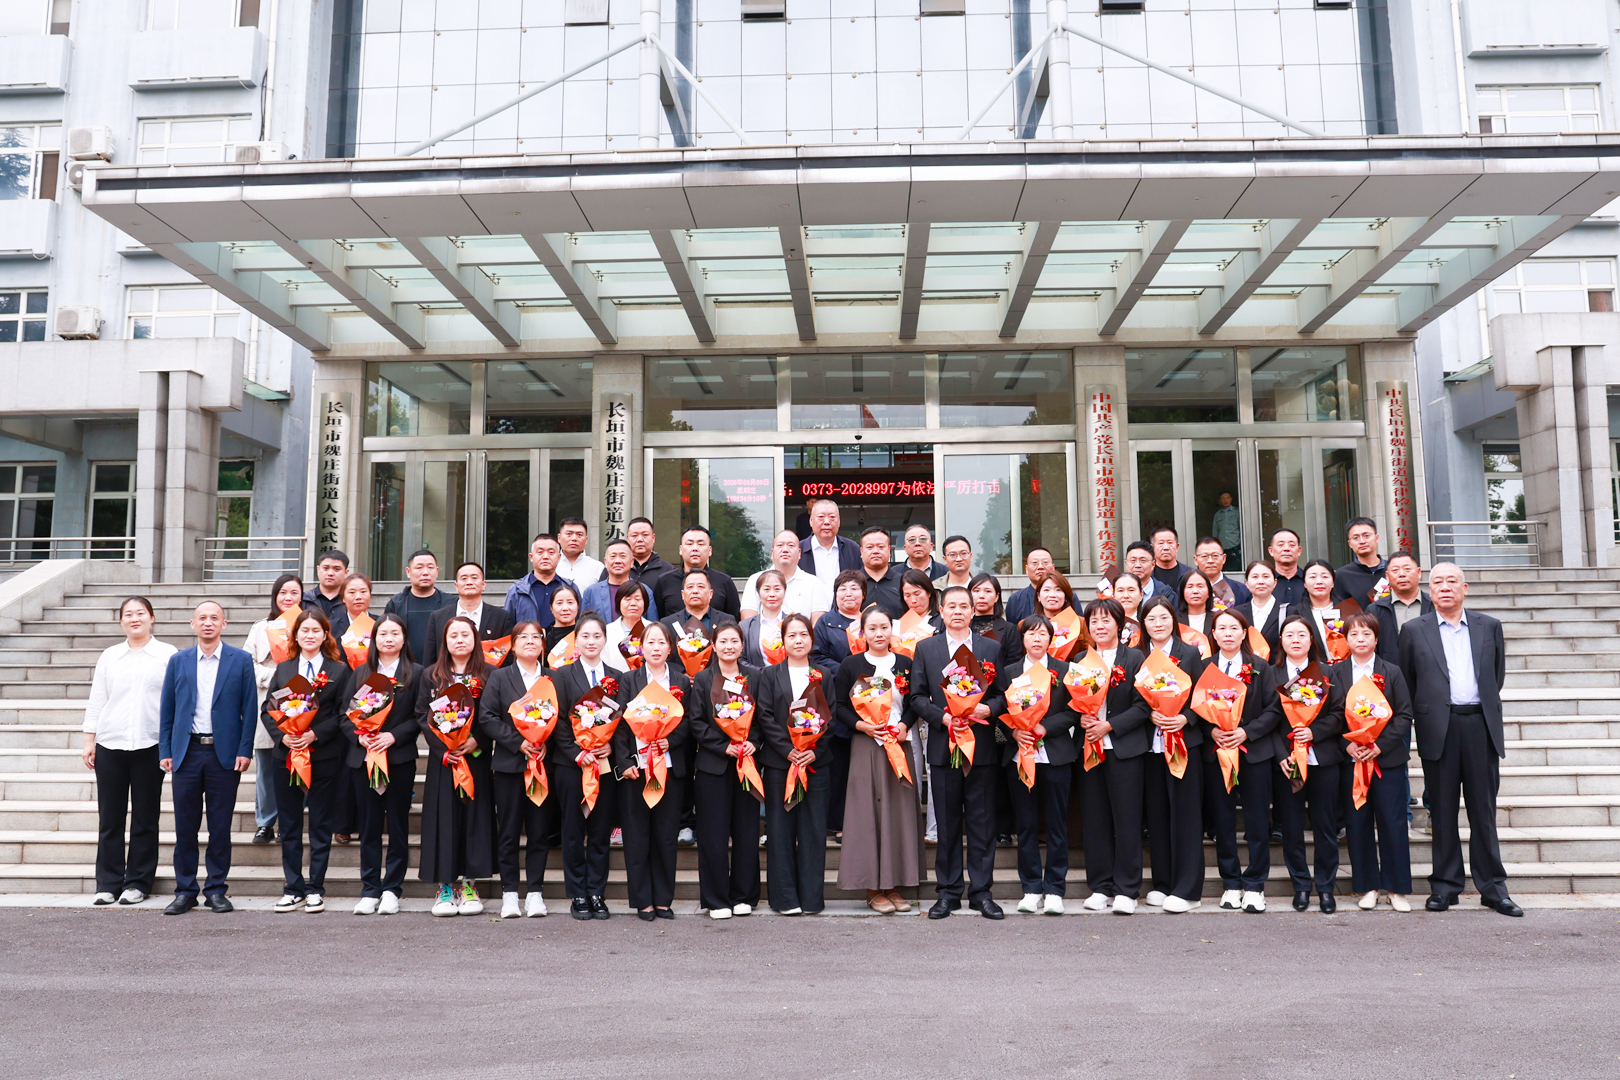
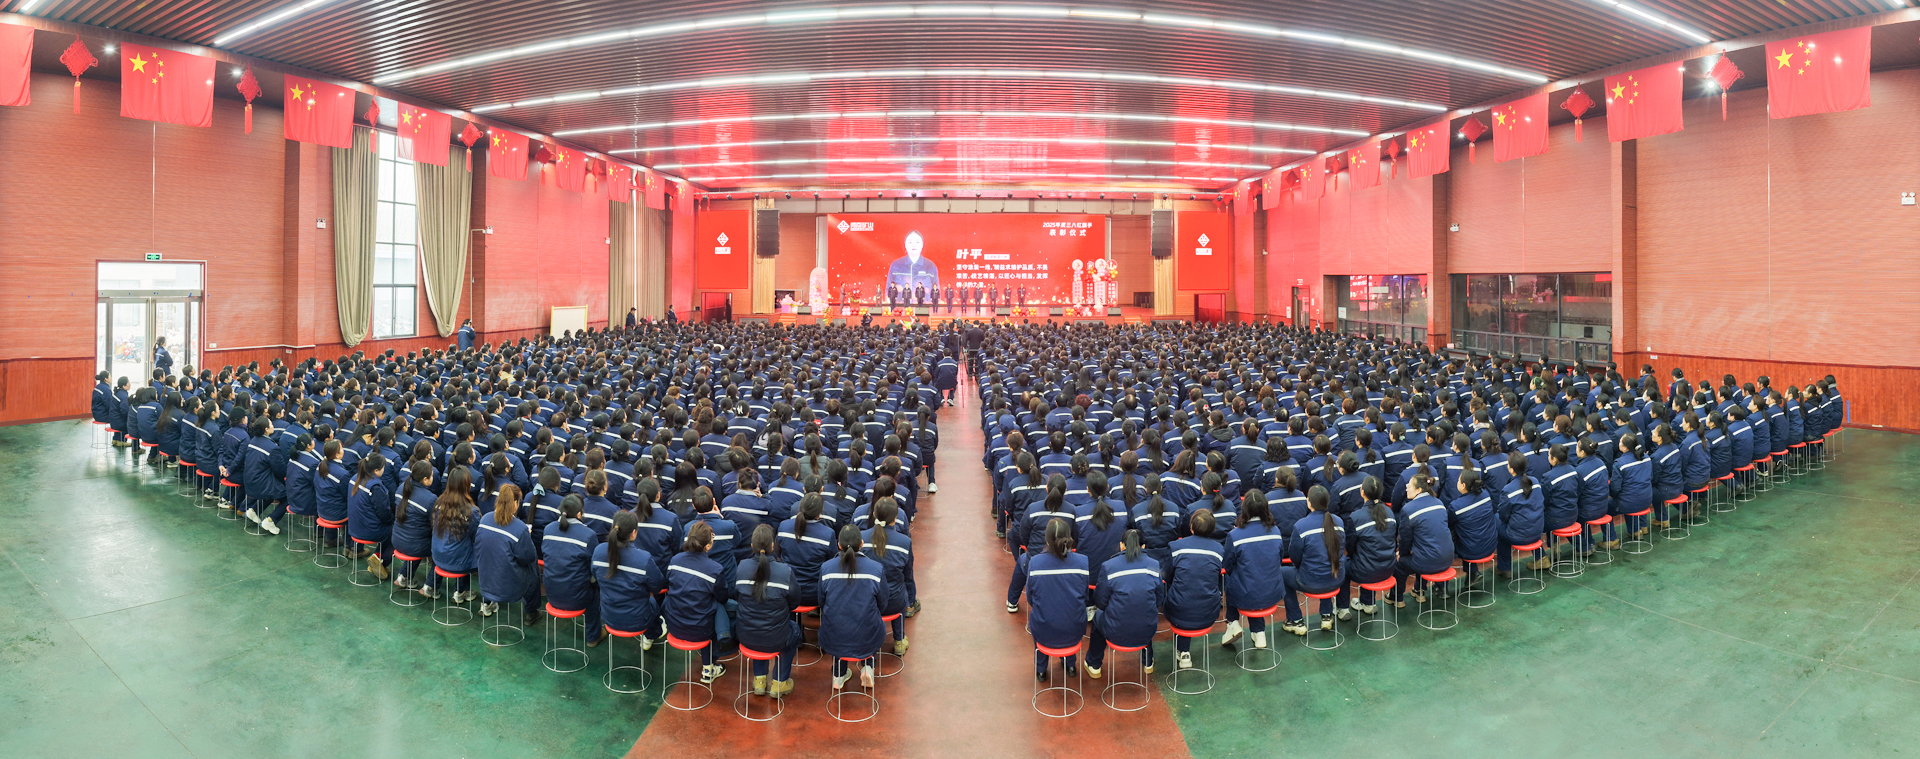
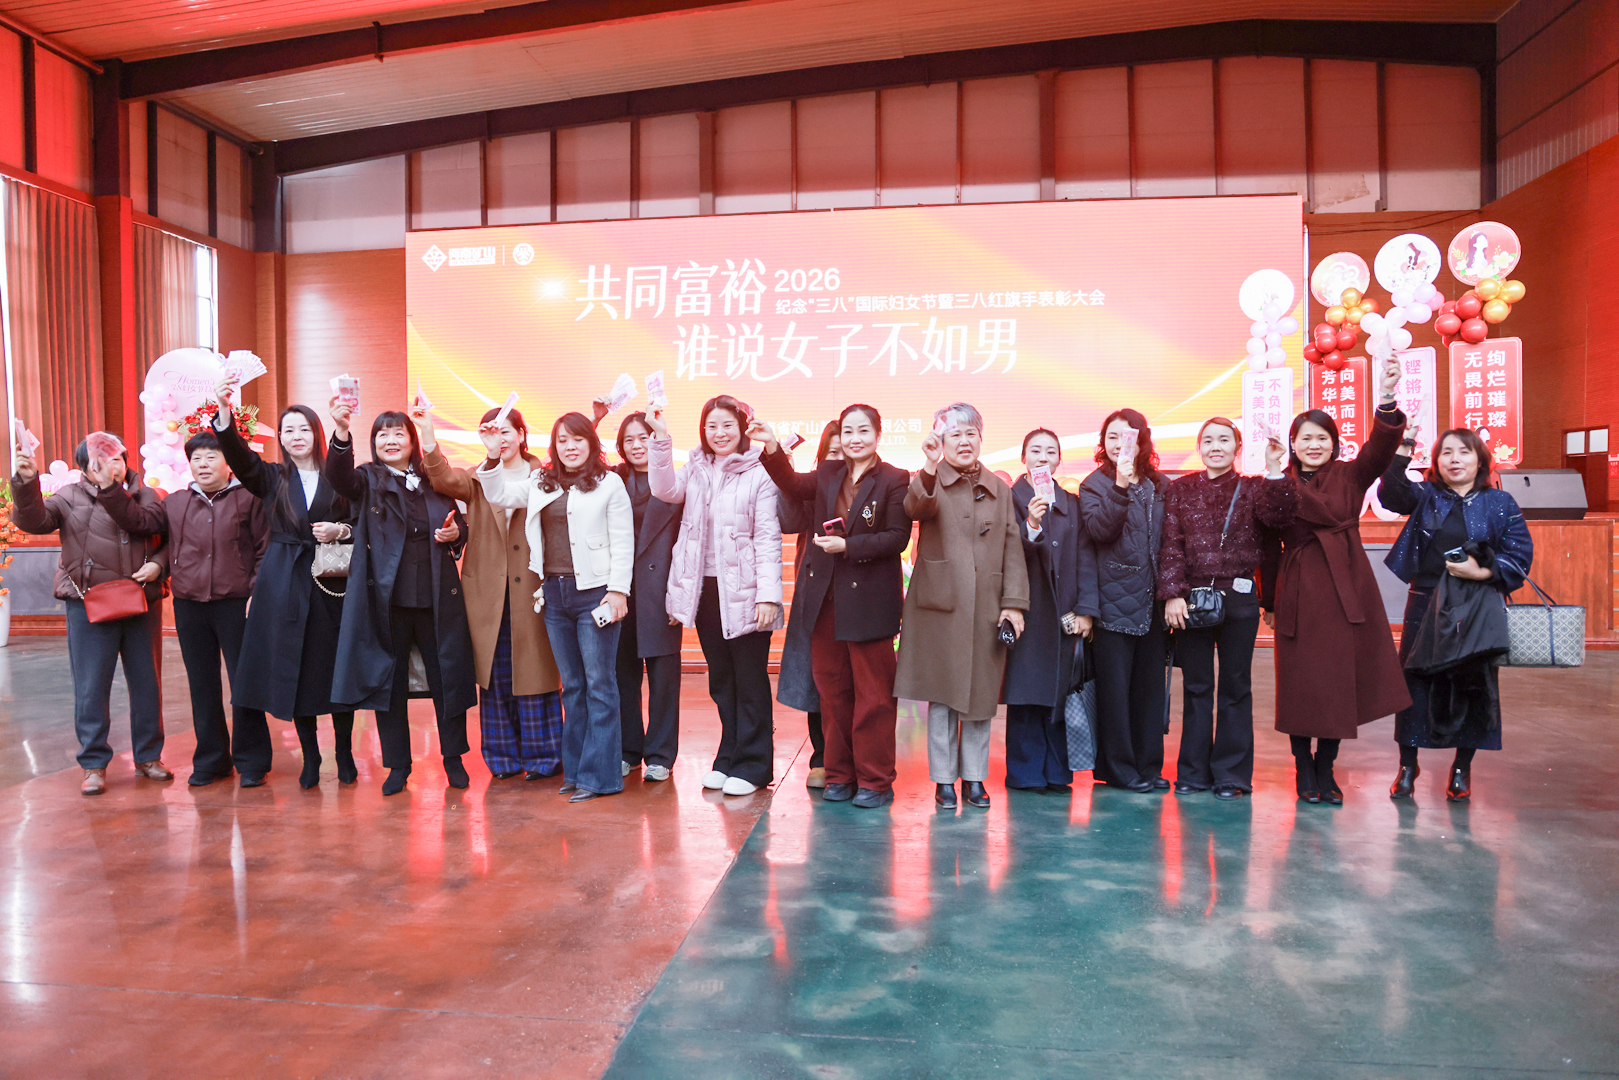
    Henan Mine Crane held an employee-recognition event on 7 March 2026 at the intelligent industrial park, ahead of International Women’s Day.

    Employees gathered for the Women’s Day recognition event at Henan Mine Crane
    Employees gathered for the Women’s Day recognition event.

    Recognition and holiday benefits

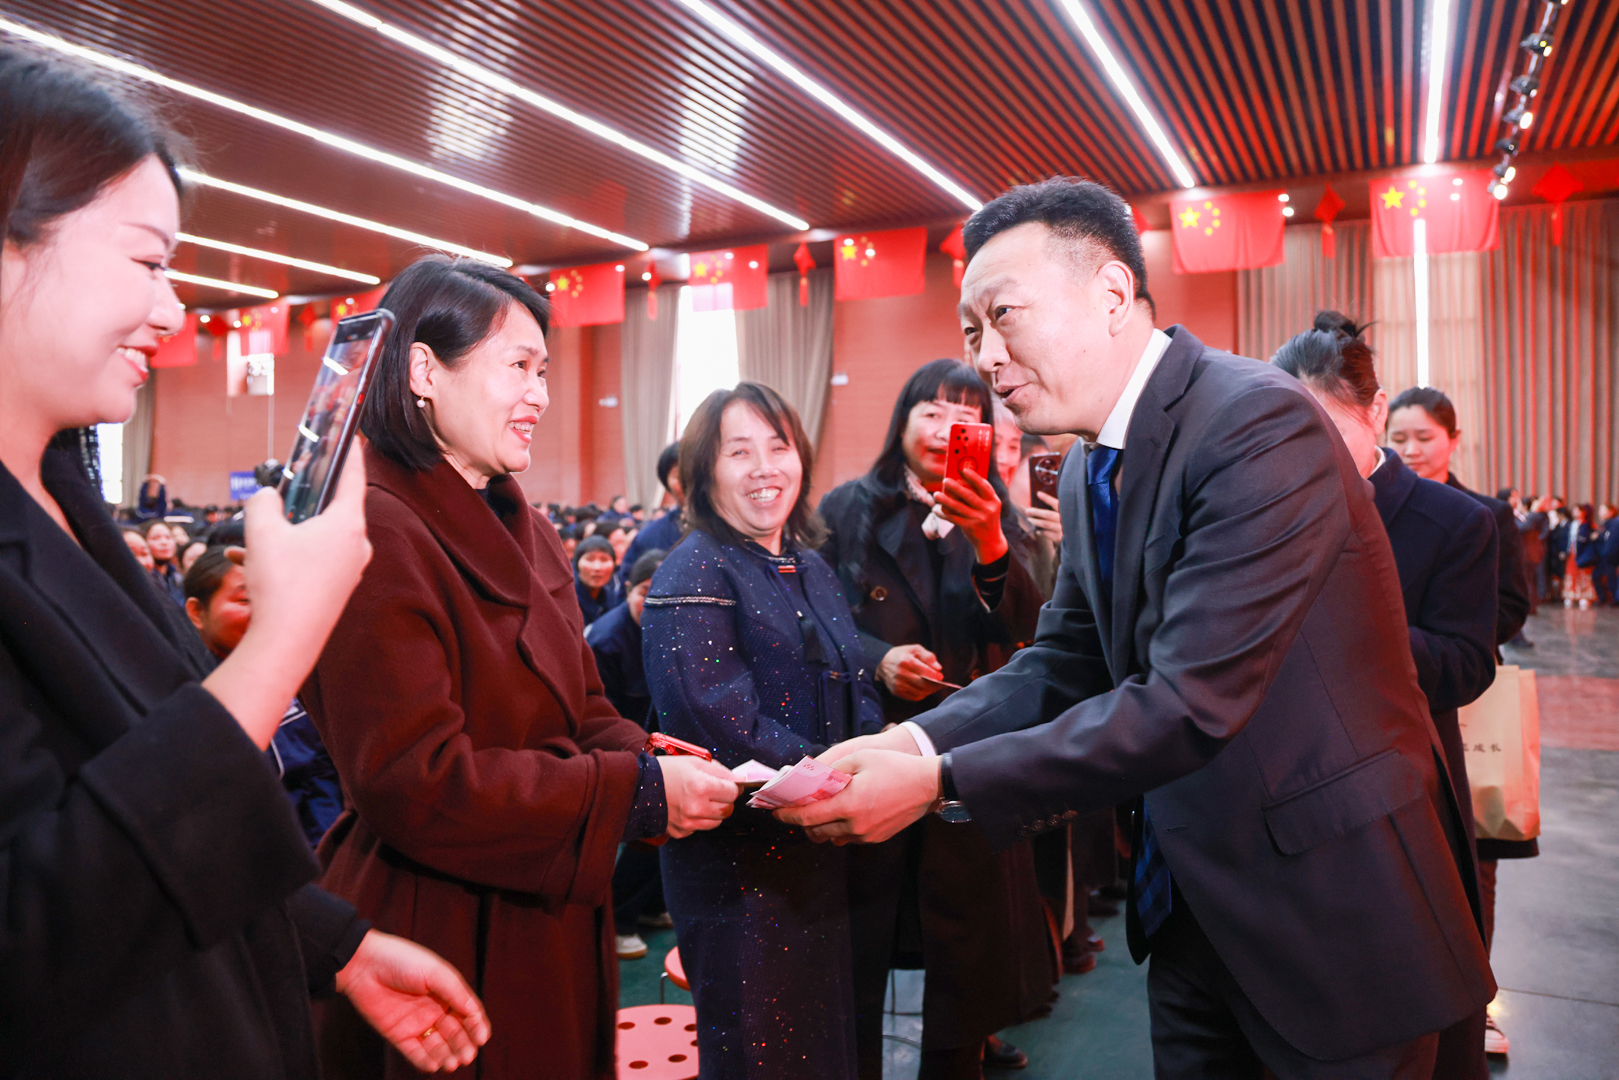
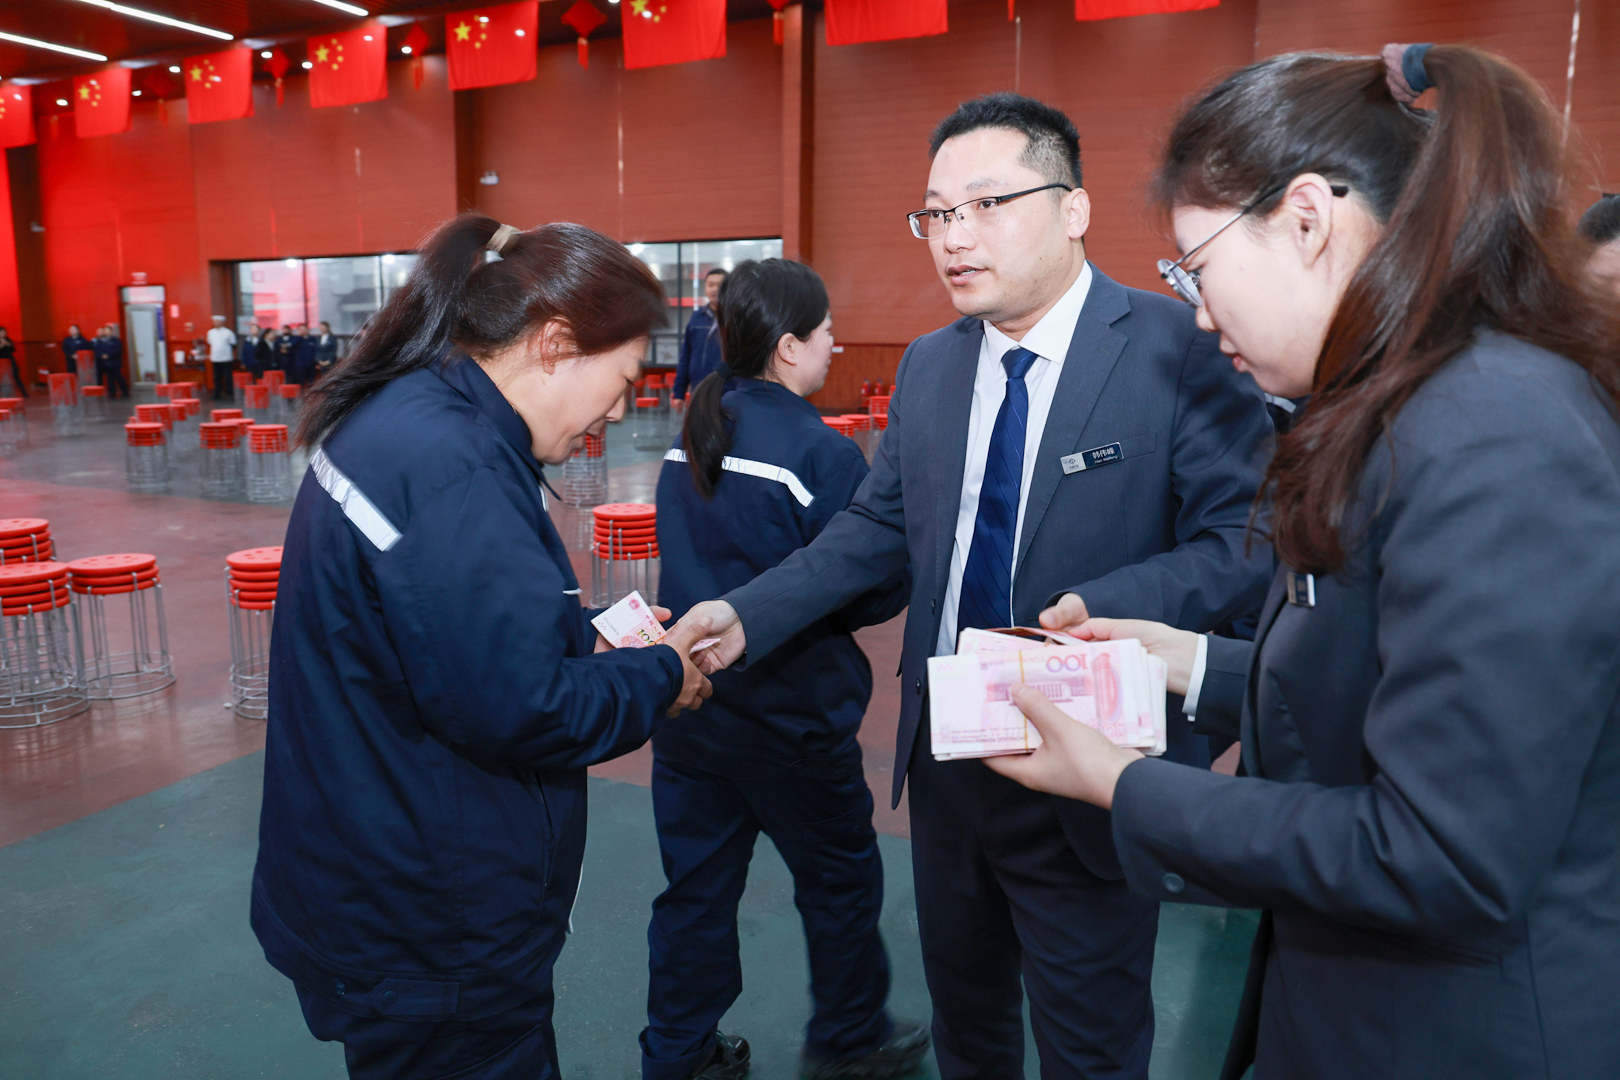
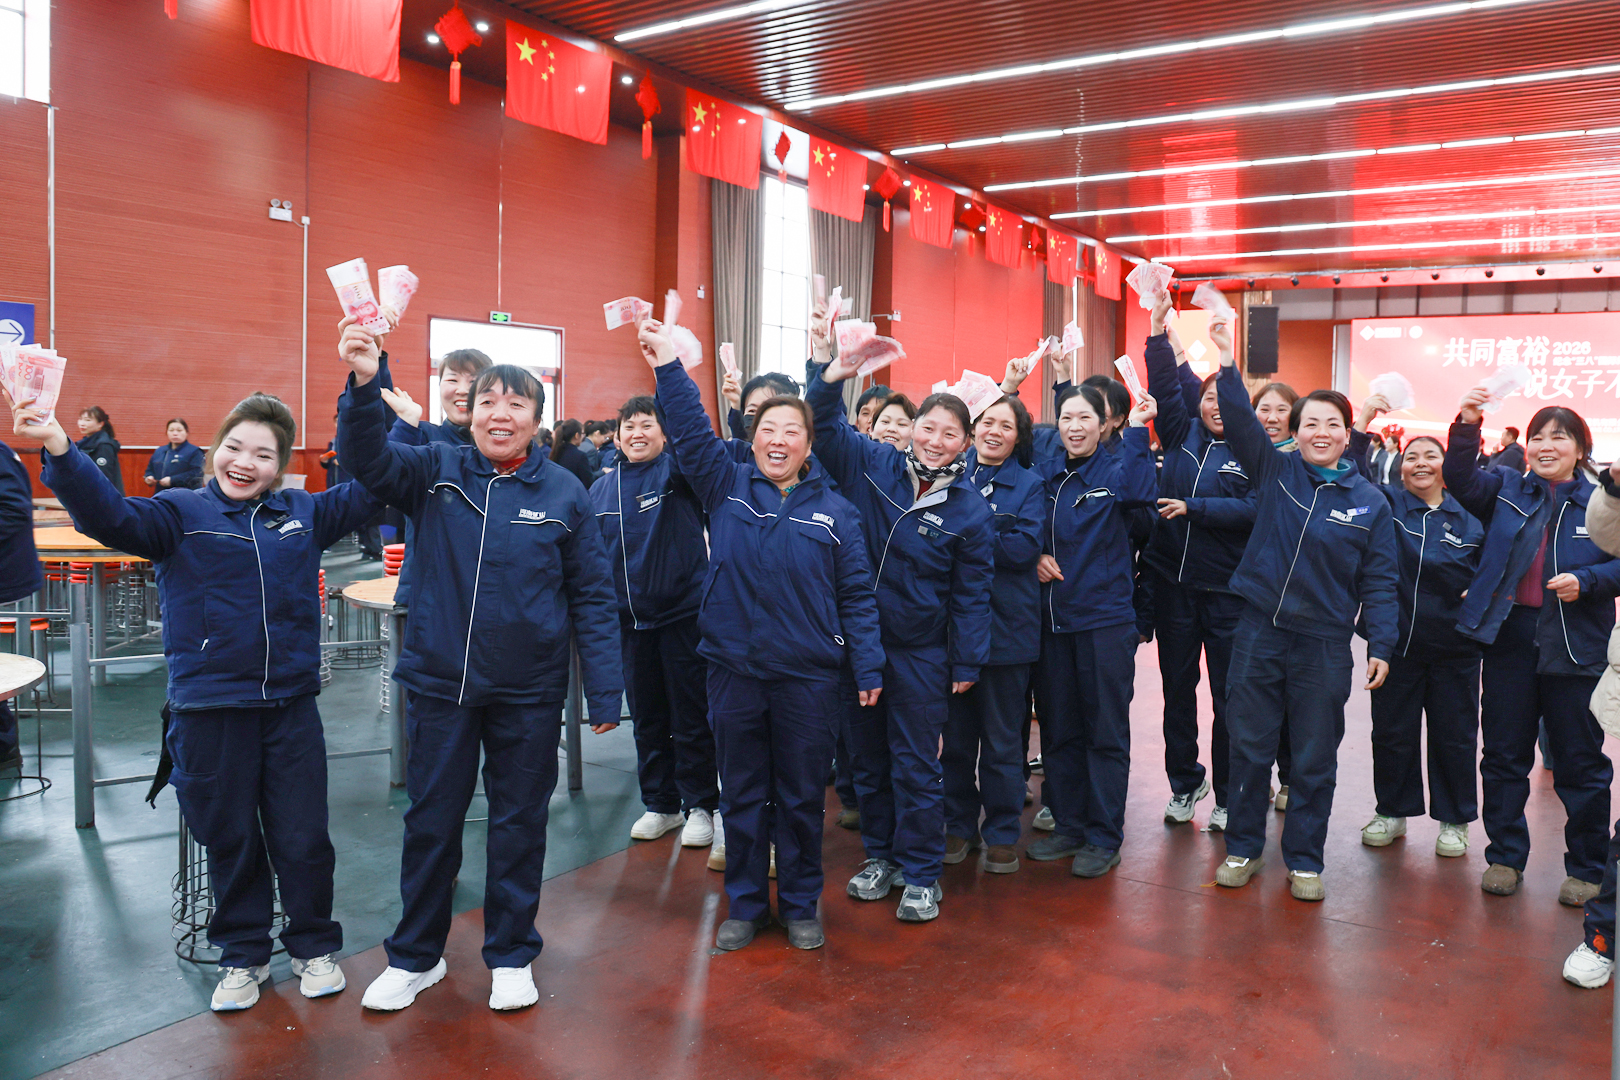
    Fourteen employees received recognition, with CNY 2,000 awarded to each. Nearly 2,000 women employees received CNY 800 each together with holiday gifts.

    Participation across company roles

    The programme included speeches, employee performances and the introduction of a new women’s committee team. Photographs record the recognition ceremony and benefit distribution.

    View the event photo gallery

    Contact Henan Mine Crane

    For product information, a manufacturing visit or a company enquiry, send the relevant details to our team.

  • Quayside Container Crane Protection: Systems to Define in the RFQ

    Quayside Container Crane Protection: Systems to Define in the RFQ

    Technical guide

    Quayside Container Crane Protection: Systems to Define in the RFQ

    Protection functions need to reflect the crane motions, surrounding equipment and terminal operating method. Describe vessel interaction, travel routes and automation boundaries so the proposed systems can be reviewed as one arrangement.

    Henan Mine CraneTechnical guide · Updated 2026Crane selection, project scope and operating requirements
    Quayside Container Cranes Henan Mine Crane factory
    Quayside Container Cranes Henan Mine Crane factory
    Project planning notes

    Key points for this crane project.

    1. Why Safety Systems Are Critical for Quayside
    2. Essential Safety Systems Every Quayside Container
    3. The Real Cost of Inadequate Safety Systems
    Read the technical guide

    Why Safety Systems Are Critical for Quayside Container Cranes

    The High-Risk Environment of Container Ports

    Container terminals are among the most demanding industrial environments in the world for lifting equipment. Quayside cranes routinely operate 24 hours a day, seven days a week, in a workspace shared by trucks, straddle carriers, AGVs, lashing crews, and pedestrian workers, often just meters from a moving crane structure.

    • High-speed trolley movement: trolleys travel the length of the boom at several meters per second to maximize crane productivity
    • Continuous 24/7 operation: constant duty cycles accelerate wear on brakes, ropes, and structural components
    • Personnel and vehicle interaction: ground crews, lashing gangs, and vehicle traffic operate directly beneath and around the crane's working envelope

    Unlike a fixed factory crane operating in a controlled environment, a quayside crane's "workspace" changes with every vessel call: different ship geometries, different stack heights, different weather, and different crews. Henan Mine Crane manufactured STS crane that safely worked a Panamax vessel in calm conditions the previous week may face a ULCS with a completely different cell-guide layout and gusting coastal winds the next.

    The scale of the equipment itself adds another layer of risk. That physical separation between the person making decisions and the point where those decisions take effect is a fundamental safety challenge that every system on this list is, in some way, designed to close.

    Common Hazards on Quayside Container Cranes

    Understanding what can go wrong is the starting point for specifying the right safety systems. The most frequently documented hazard categories include:

    • Container collisions:with the ship's cell guides, hatch covers, or adjacent stacks
    • Crane-to-crane collisions:when multiple cranes work the same vessel in tandem
    • Overloading:from misjudged container weights, twin-lift errors, or snagged loads
    • High wind conditions:the single largest cause of catastrophic quayside crane loss globally
    • Mechanical failures:brake, rope, or gearbox faults from fatigue and salt-air corrosion
    • Human error:misjudged clearances, procedural shortcuts, and fatigue-related mistakes
    • Electrical faults:short circuits, arc flash events, and grounding failures in the crane's high-voltage systems

    Benefits of Comprehensive Safety Systems

    A well-specified safety architecture pays for itself well beyond accident prevention. Terminals that invest in comprehensive, integrated safety systems typically see:

    • Improved operational reliability:fewer unplanned stoppages caused by near-miss incidents or safety-triggered shutdowns
    • Lower maintenance costs:early fault detection prevents small issues from becoming major structural or mechanical repairs
    • Reduced accident rates:fewer lost-time injuries and equipment damage claims
    • Increased terminal productivity:automated safety interlocks reduce the conservative, "better safe than sorry" slowdowns operators apply when they don't trust the equipment

    Insurance and risk-management data from the marine cargo and port equipment sector consistently identifies wind damage as the single largest weather-related cost category for quayside cranes, and structural or tie-down failures, not routine mechanical wear , as the leading cause of total crane losses. That single data point underscores why comprehensive safety system coverage isn't a marginal improvement; it directly determines whether a multi-million-dollar asset survives its full design life or becomes a total loss during one severe weather event.

    Essential Safety Systems Every Quayside Container Crane Should Have

    Henan Mine Crane modern STS crane is not protected by a single safety feature, it relies on a layered architecture of independent systems, each covering a different failure mode. Below are the systems considered essential on any quayside container crane specified today.

    Anti-Collision System

    Anti-collision protection is arguably the most safety-critical system on a quayside crane, given how close cranes, ships, and trolleys operate to one another. A modern anti-collision system typically includes:

    • Crane-to-crane collision prevention:sensors that detect the position of adjacent cranes on the same rail and automatically slow or stop travel before contact
    • Trolley collision avoidance:preventing the trolley from over-traveling into end stops or other equipment on the boom
    • Ship structure protection:preventing the boom or spreader from striking the vessel's cell guides, hatch coamings, or superstructure
    • Automatic slowdown and stopping:graduated deceleration zones rather than a single hard stop, which reduces mechanical shock loading
    • Laser, radar, LiDAR, and sensor technology:the detection layer that feeds real-time distance data into the crane's control system

    These systems are particularly important in automated and semi-automated terminals, where multiple cranes may be commanded by a central scheduling system rather than individually supervised by an operator in each cab.

    Overload Protection System

    Overloading is one of the most direct threats to both personnel safety and structural integrity. Overload protection systems combine several layers of monitoring:

    • Real-time load monitoring:continuous measurement of the load on the hoist via load cells or strain gauges
    • Safe working load limits:hard-coded thresholds tied to the crane's rated capacity
    • Load moment protection:accounting for both load weight and outreach position, since the moment (not just the weight) determines structural stress
    • Protection against structural damage:preventing cumulative fatigue damage to the boom, girder, and rope system from repeated overload events

    Because container weights are frequently misdeclared or estimated, overload protection is one of the systems most likely to be triggered in daily operation, making its calibration and reliability essential.

    Wind Monitoring and Storm Protection

    Industry loss data consistently identifies wind as the single biggest cause of catastrophic quayside crane damage, more so than mechanical failure, overload, or collision combined. Insurer analyses of storm-related crane losses have repeatedly found that failure originates not in the main structure, but in the tie-down and stowage-pin systems meant to secure the crane when out of service. A complete wind protection package includes:

    • Anemometers:real-time wind speed sensors mounted on the crane structure, feeding continuous data to the operator and control system
    • Storm parking mode:a predefined, manufacturer-specified position for the trolley, boom, and structure when the crane is taken out of service ahead of severe weather
    • Rail clamps:mechanical or hydraulic devices that grip the crane rail to prevent uncontrolled travel in high winds
    • Tie-down systems:chains, slings, or turnbuckles connecting the crane's four corners to anchor points embedded in the quay pavement
    • Anchoring devices:stowage pins and supplementary anchors designed to hold the crane stationary against extreme, storm-force wind loads

    Because most quayside cranes are designed to a specific design wind speed with a defined recurrence interval, terminals in typhoon-, hurricane-, or cyclone-prone regions should periodically reassess whether current and forecast wind conditions still fall within the original design assumptions, particularly after any crane modification such as leg raising or boom extension.

    Emergency Stop (E-Stop) System

    The emergency stop system is the crane's last line of defense when any other safety system fails to prevent an unsafe condition. A properly specified E-stop architecture includes:

    • Multiple emergency stop buttons:positioned at every operator and maintenance access point
    • Remote emergency shutdown:allowing ground personnel or terminal control room staff to halt the crane without needing cab access
    • Operator cabin controls:a primary E-stop within immediate reach of the operator's seat
    • Ground-level emergency controls:accessible to lashing crews and maintenance staff working beneath the crane
    • Restart procedures:a controlled, deliberate re-energization sequence that prevents accidental restart before the hazard is cleared

    Limit Switch Protection

    Limit switches are electromechanical or electronic devices that prevent crane components from traveling beyond their designed range of motion. On a quayside crane, this includes:

    • Hoist upper/lower limits:preventing the spreader from over-hoisting into the boom structure or over-lowering into the ship's hold
    • Trolley travel limits:stopping the trolley before it reaches the end of the boom or backreach rail
    • Gantry travel limits:preventing the entire crane from traveling beyond the end of the quay rail
    • Boom luffing limits:controlling the raising and lowering of the boom during stow and deploy sequences
    • Preventing over-travel accidents:the cumulative function of all limit switches working together to keep every motion axis within its safe envelope

    Rope Monitoring System

    The hoisting wire rope is a critical, high-wear component subject to constant load cycling, and its failure can be catastrophic. Rope monitoring systems typically provide:

    The Real Cost of Inadequate Safety Systems

    Before moving into the technology itself, it's worth quantifying why this matters commercially, not just operationally. A single crane collapse or major structural failure typically results in:

    • Total or near-total loss of the crane:quayside cranes routinely cost several million dollars each, and structural failures are rarely economical to repair
    • Extended berth downtime:a lost crane at a busy terminal can mean weeks or months of reduced throughput while replacement or major repair is arranged
    • Collateral damage:falling structures, swinging booms, and uncontrolled crane travel frequently damage adjacent cranes, vessels, and quay infrastructure
    • Regulatory and insurance consequences:incidents involving inadequate or poorly maintained safety systems can affect insurability and invite regulatory scrutiny of the entire fleet

    Engineering investigations into historical crane collapses have repeatedly found that the initiating failure was not the crane's primary structure, which is typically over-engineered relative to normal operating loads, but rather secondary systems such as tie-downs, stowage pins, or wheel brakes that were undersized, poorly maintained, or simply not deployed in time. This is a critical insight for procurement and maintenance teams: the systems most likely to determine whether a crane survives a major event are often the ones that receive the least day-to-day attention, precisely because they are rarely used.

    Smart Safety Technologies in Modern Automated Container Terminals

    As terminals move toward semi-automated and fully automated operations, safety technology has evolved beyond mechanical and electromechanical devices into intelligent, data-driven systems.

    AI collision avoidance takes the concept of distance sensors a step further; it incorporates machine learning based on data gleaned from terminal trajectories in order to avoid collision before it becomes imminent, rather than reacting to a set threshold.

    An engineered digital twin monitor generates a real-time virtual representation of the machine’s structural and mechanical health, which engineers can then utilize to simulate stress conditions and discover anomalies without having to check each individual element on-site.

    Predictive maintenance relies on monitoring the trends of sensors – vibration, temperature, current draw, detecting a developing problem so that failure can be anticipated, rather than scheduled.

    The individual data points from hundreds of sensors located throughout the crane are combined into a centralized system that cross-references the readings, possibly revealing a problem before it occurs.

    Remote monitoring of cranes enables engineering and safety teams (including maintenance support from the manufacturer) to investigantry crane health details from another location, allowing faster diagnosis and less downtime.

    Real-time health diagnostics provide a quick-up picture of the health status of each of the major subsystems, as opposed to requiring periodic human visual inspection.

    Auto-fault Messages, enable the automatic notification of out of range readings to the responsible maintenance or safety engineer without the need to wait until the next scheduled inspection.

    These smart technologies by themselves are not to suggest replacing the mechanical and electrical safety systems mentioned earlier; rather they provide an additional layer of prediction that can identify degradation before the safety event occurs.

    International Safety Standards for Quayside Container Cranes

    Adherence to recognized engineering standards isn’t simply a regulatory checkbox it’s the rule by which a crane’s safety systems are engineered, tested, and maintained to a common, reliable standard.

    ISO Standards for Container Cranes

    The classification of cranes by duty cycle and load spectrum as defined by ISO 4301 translates directly into design margins for structural parts, brakes and ropes. This classification allows two cranes of equal lifting capacity to operate with quite different safety margins depending on the load spectrum used an important consideration, for example, for high throughput, around the clock terminals versus lower velocity feeder ports.

    FEM Design Rules

    The FEM 1.001 rules (Fédération Européenne de la Manutention) provide detailed design guidance for hoisting appliances and remain widely referenced in Henan Mine Crane STS crane structural engineering, even where regional standards have since evolved. Many quayside cranes still in service today were originally designed under FEM guidance, which is why understanding this legacy framework remains relevant for fleet audits and modification projects.

    IEC Electrical Safety Standards

    The electrical control system, motor drives and protection devices fitted on every quayside crane are governed by IEC standards, providing an equal level of safety performance between manufacturers and areas. This is crucial for terminals running mixed-vehicle manufacturers, where electrical safety behavior is always consistent between various quayside type and manufacturers, reducing maintenance and driver training effort.

    EN Standards for Crane Safety

    The design requirements for crane equipment listed on EN 13135 and associated EN standards. These covers safety-related design requirements for crane equipment (ranging from access equipment to control and monitoring devices.) and was then followed in 2001 by themangency of EN 13001 which adopted state of the art limit-state design as opposed to the old allowable-stress approach, so that the structural design of cranes conforms more closely to current Eurocode engineering principles.

    OSHA and Local Port Safety Requirements

    Local port authorities and municipal jurisdictions especially those in hurricane and cyclone regions often pile their own requirements for wind-design and storm readiness directives onto the OSHA federal mandates.

    Why Compliance Matters for Long-Term Reliability

    Since quayside cranes can operate over 25 to 30 years, standards-based design guarantees that safety systems, design limits, and maintenance procedures can be audited and verified not only throughout the life of the end product but also following any modification, such as boom extensions or the installation of automation retrofits.

    How to Select a Quayside Container Crane with the Right Safety Features

    Evaluate Operational Requirements

    Start with the terminal's actual operating profile: vessel sizes served, throughput targets, wind exposure, and whether automation is planned now or in the future. Safety system specification should follow directly from these operational realities, not be treated as a generic checklist. A terminal in a typhoon corridor has fundamentally different wind-protection priorities than one in a temperate, low-wind region, just as a fully automated terminal has different visibility and collision-avoidance requirements than one relying on cab-based operators for every lift.

    Verify Built-In Safety Systems

    Confirm that anti-collision, overload protection, wind monitoring, and emergency stop systems are factory-integrated rather than aftermarket additions, since integrated systems typically offer more reliable data sharing and faster response times.

    Consider Automation and Future Expansion

    Even terminals not planning immediate automation should evaluate whether a crane's control architecture can support future upgrades, retrofitting safety and automation systems onto an older control platform is significantly more costly than specifying for it upfront.

    Assess Manufacturer Experience and Technical Support

    A manufacturer's track record with safety system reliability, spare parts availability, and technical support responsiveness matters as much as the specifications on paper, particularly over a multi-decade service life.

    Preventive Maintenance for Quayside Container Crane Safety Systems

    Even the most advanced safety system is only as reliable as the maintenance program behind it. Structured inspection and testing routines are what keep these systems functioning as designed over decades of continuous, high-cycle use.

    Predictive Maintenance with Smart Monitoring

    • IoT sensors tracking vibration, temperature, and load data continuously
    • Early fault detection that flags anomalies before failure
    • Reduced unplanned downtime by shifting from reactive to condition-based maintenance

    None of these maintenance layers function in isolation. Daily checks catch the obvious, visible issues; routine functional testing verifies that safety systems still respond correctly under real conditions rather than just passing a self-diagnostic; and predictive monitoring catches the slow, gradual degradation that neither daily inspection nor periodic testing would reveal in time. Terminals that rely on only one of these three layers, for example, daily checks without routine functional testing, tend to discover safety system failures only after they've already caused an incident or a costly unplanned shutdown.

    It's also worth noting that maintenance records themselves are a safety asset. Documented inspection histories, wind-event logs, and repair records provide the evidence base needed to validate that a crane's safety systems have performed as designed throughout its service life, information that becomes critical during insurance claims, regulatory audits, and end-of-life structural assessments.

    Why Safety System Integration Matters More Than Individual Devices

    A crane equipped with excellent individual safety devices can still be unsafe if those devices don't communicate with one another. Integration is what turns a collection of sensors into a coherent safety architecture.

    Data Sharing Between Safety Systems

    If the overload data, wind speed, and collision-proximity values can be communicated system-to-system, then the control logic aboard the crane can respond smarter for example, automatically tightening collision-avoidance margins when wind speed exceeds a selected threshold, or modifying sway-control parameters so they are more appropriate for the current load weight instead of using them default at a given value. This is the sort of inter-system information sharing that distinguishes true intelligent safety architecture from a collection of separate devices that have all solved their problems but may have no knowledge that they are bound together.

    Real-Time Diagnostics and Alarm Management

    Effective integrated alarm management safeguards against “alarm fatigue,” in which operators are overwhelmed by large quantities of inconsequential alarms and fail to respond to an important alarm.

    Reducing Operator Workload

    Good integrated systems perform most of the safety checks and interlocks automatically. The operator is able to concentrate his attention on the lift rather than dozens of independant readouts.

    Improving Equipment Reliability and Terminal Efficiency

    Integration also has benefits for safety as well as improved throughput performance for example, benefits in terms of reduction in false-trigger shutdowns and unnecessary conservative slowdowns in terms of achieving terminal throughput rate targets.

    Choosing a Quayside Container Crane with Advanced Safety Systems

    Evaluate Safety Certifications and Compliance

    Verify that the crane design and build are certified to ISO, EN, FEM and regional regulatory codes, and obtain evidence rather than manufacturer‘s marketing speak.

    Assess Intelligent Safety Technologies

    Focus on the future to include AI-enabled collision avoidance, digital twin monitoring, and predictive maintenance features that prolong the life of the crane and the safety systems.

    Consider Future Upgrade Capabilities

    Verify that the existing control architecture, sensor network, are compatible with future increases in automation levels and/or safety system upgrades so a new control system will not be necessary.

    Partner with an Experienced Crane Manufacturer

    A manufacture’s engineering track record withsafety system design, ie, how theircranesperformed under actual storm events and high cycle operations, can speak volumes to theirlong term reliability. Request references from terminals under similar climatic and throughput conditions, and see if they have documented performance or if they are just quoting published specifications.

    Questions to Ask Before Purchasing

    • Does the crane comply with international safety standards?
    • Can safety systems be upgraded in the future?
    • How are spare parts and after-sales service provided?

    Henan Mine Crane

    Today no single anti-collision device can claim to define quayside container crane safety an integrated safety architecture of anti-collision, overload, wind, intelligent diagnostics, predictive maintenance and internationally approved design and safety systems, is increasingly the overall defining factor. Achieving global safety and reliability standards from the outset allows terminals to mitigate risks and delays, and maximize equipment and port productivity.

    Innovative crane technology and international project history will enable the industry partner to enhance automated safety, efficiency and productivity in the long term.

    Frequently Asked Questions

    What safety systems are essential for a quayside container crane?

    The essential systems include anti-collision protection, overload monitoring, wind and storm protection (including tie-downs and rail clamps), emergency stop networks, limit switches, rope monitoring, electrical protection, operator visibility systems, fire detection, and safe access infrastructure. These work together as a layered safety architecture rather than standalone features, no single system is designed to catch every failure mode, which is exactly why terminals should evaluate the completeness of the full set rather than the strength of any one device in isolation.

    How does an anti-collision system work on an STS crane?

    Anti-collision systems employ laser, radar, LiDAR or other proximity sensors to monitor the spacing between the crane, neighboring cranes, ship and terminal equipment at all times. Upon arriving at a predetermined point, graduated deceleration and/or (if necessary) full stop before impact is commenced.

    What wind speed is considered unsafe for container crane operations?

    Storm parking and tie-down operations will usually be initiated at a wind speed well below the maximum survival design speed of the crane.

    Why is overload protection important for ship-to-shore cranes?

    Overload protection prevents structural damage from loads exceeding the crane's rated capacity, which can occur due to misdeclared container weights or twin-lift errors. Beyond the immediate risk of rope or structural failure, repeated overload events cause cumulative fatigue damage that shortens the crane's operational lifespan.

    How often should quayside container crane safety systems be inspected?

    Functional and visual inspection of the main safety devices (E-stops, brakes, wire ropes) on a daily basis are undertaken as a norm. Additionally scheduled routine inspection is undertaken on anti-collision/overload /limit switch/wind monitor systems and continual predictive monitoring is conducted via IoT sensor systems for which they are installed.

    Predictive maintenance uses continuous sensor data, vibration, temperature, load cycling — to identify component degradation before it results in failure, shifting maintenance from a fixed calendar schedule to a condition-based approach that catches problems earlier and reduces unplanned downtime.

    Discuss the crane arrangement for your project.

    Protection functions need to reflect the crane motions, surrounding equipment and terminal operating method. Describe vessel interaction, travel routes and automation boundaries so the proposed systems can be reviewed as one arrangement. Share the load, available drawings, working cycle and site conditions with Henan Mine Crane so the required configuration and supply boundary can be discussed.

    Related crane configurations

    Container Overhead Crane

    View product parameters
    Lifting capacity: 30-65 tSpan: 18-35 mLifting height: 8 – 20 m

    Transfer containers within a defined overhead runway area using a double-girder bridge and matched spreader. Container size, working clearance and the handling sequence determine the arrangement.

    Container Straddle Carrier

    View product parameters
    Lifting capacity: 30 – 50 tStacking arrangement: 1 over 3 – 1 over 6Working class: A7 – A8

    Move containers between handling positions with a straddle carrier matched to the travel route and stacking layout. Define container load, ground conditions, clearance and the preferred drive system.

    Updated 2026 · Henan Mine Crane
  • Henan Mine Crane Donates CNY 200,000 to Support Local Teachers
    Henan Mine Crane Donates CNY 200,000 to Support Local Teachers
    Company & People

    Henan Mine Crane Donates CNY 200,000 to Support Local Teachers
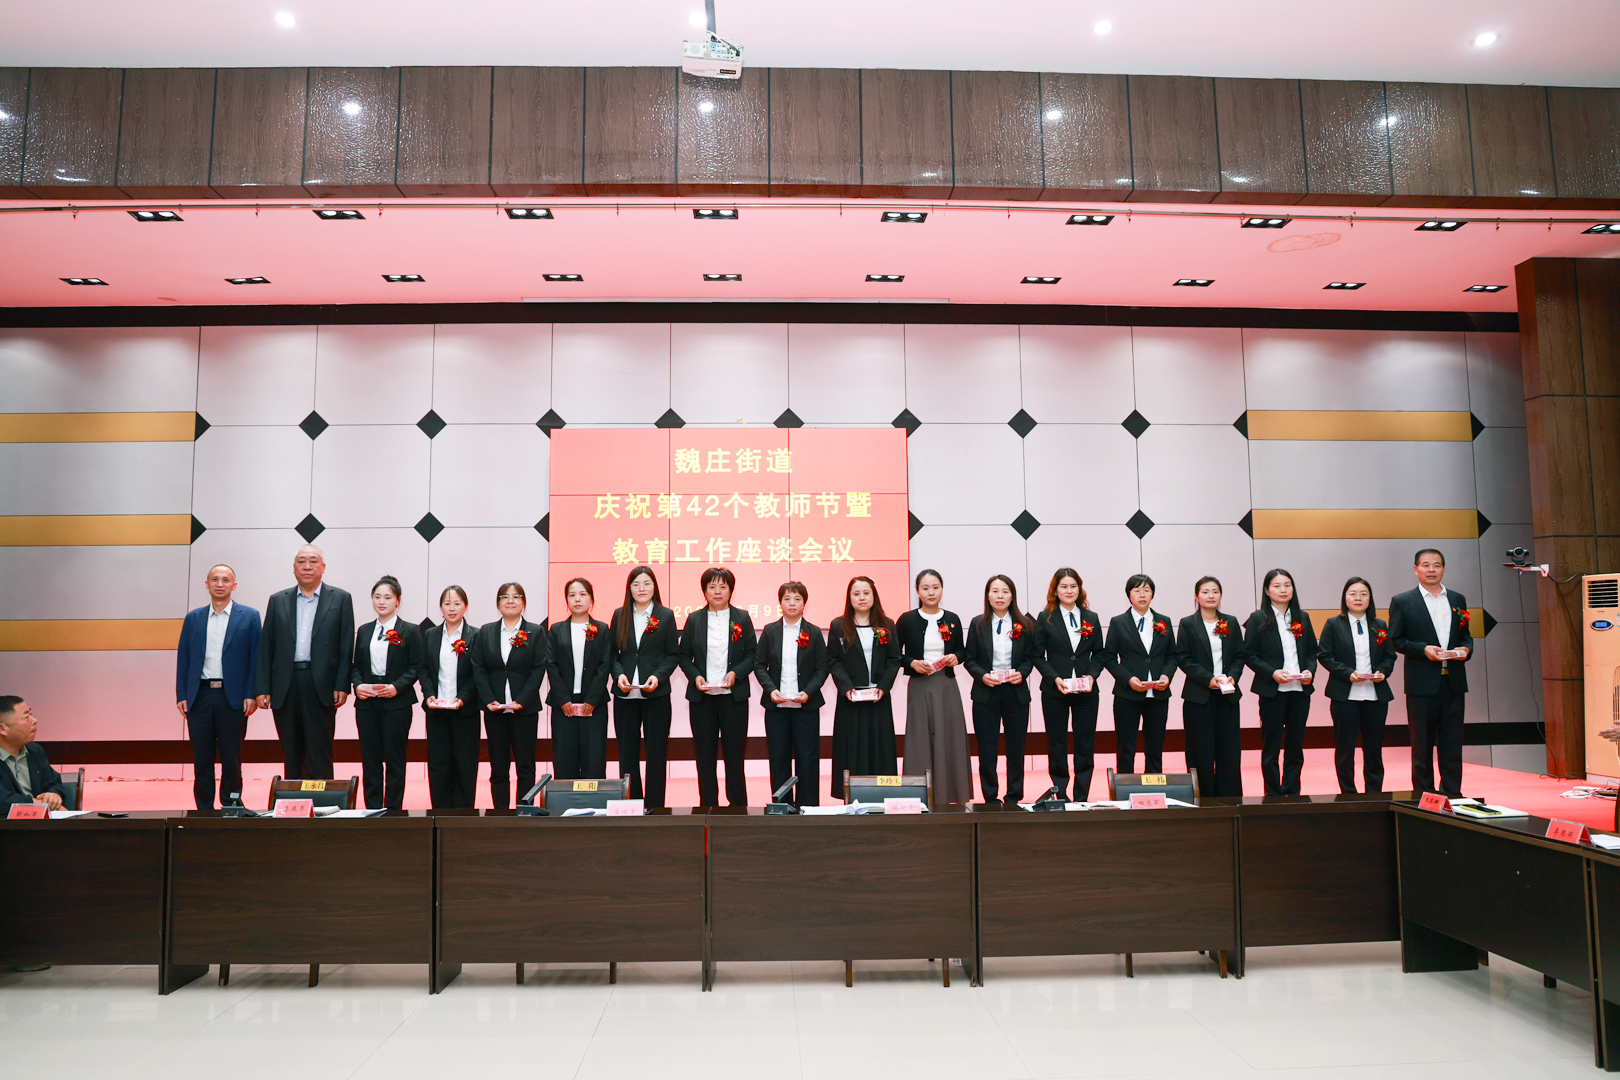
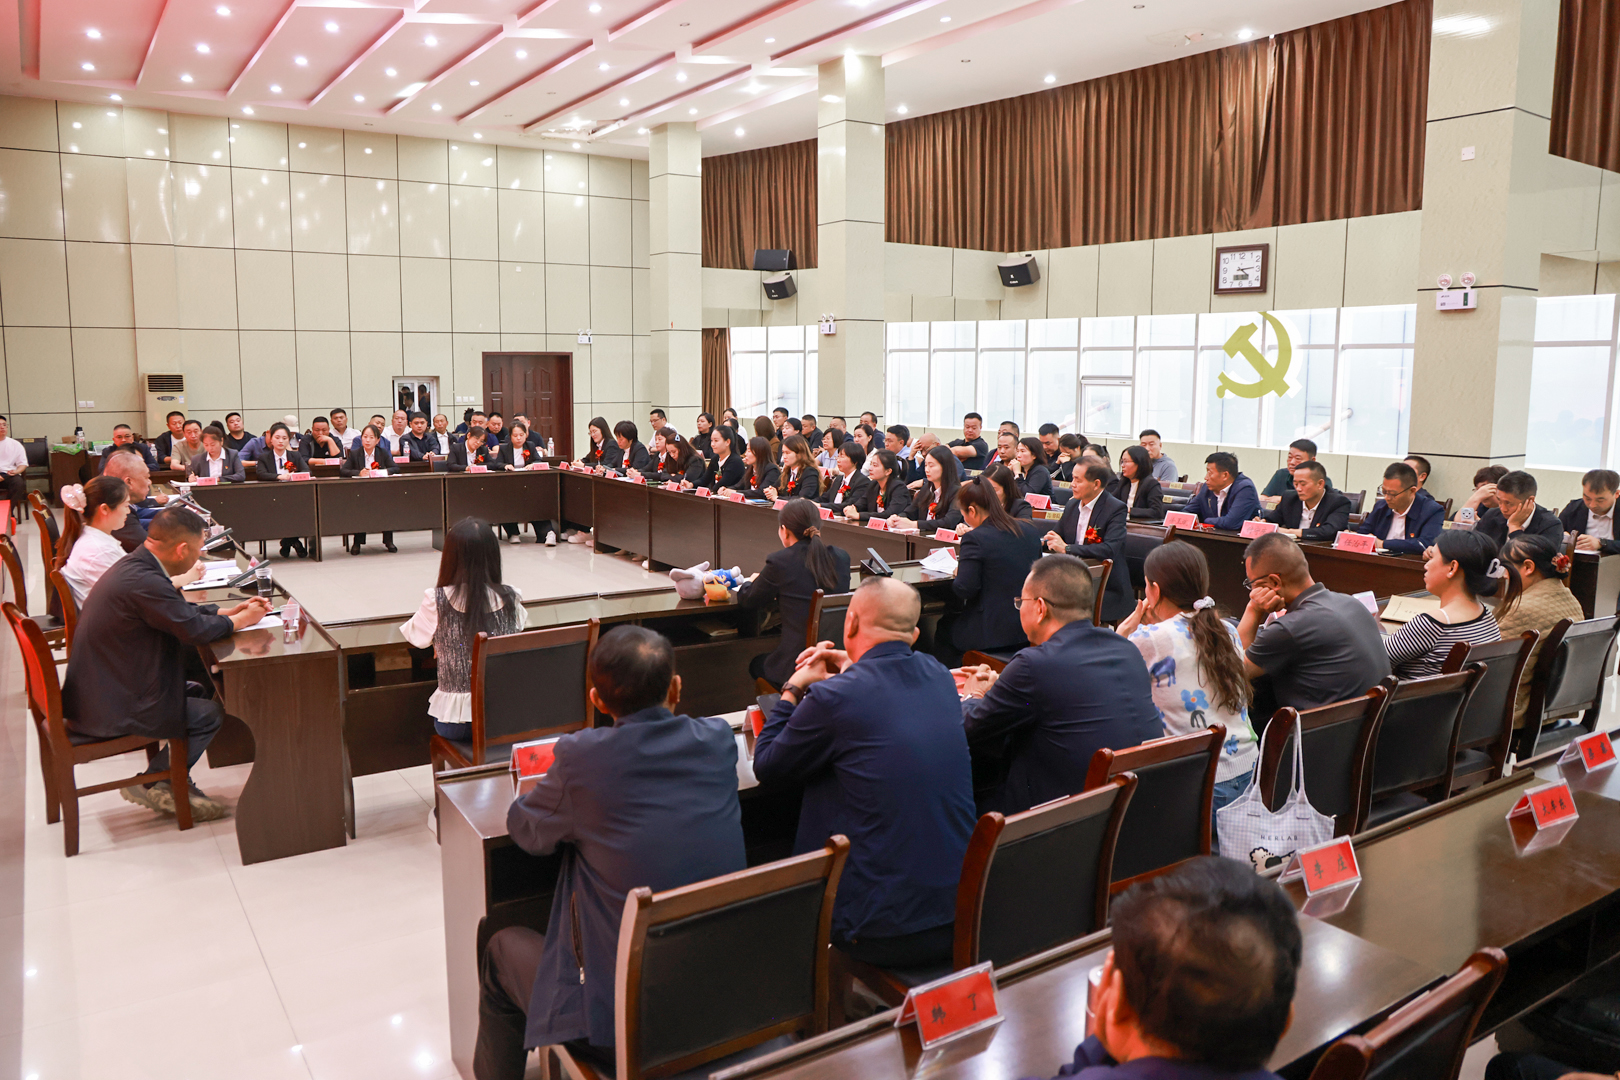
    Henan Mine Crane donated CNY 200,000 to the Weizhuang education system during a Teachers’ Day education meeting on 9 September 2026.
    Education meeting in the Weizhuang conference hall
    Education meeting in the Weizhuang conference hall.

    Funding for teacher recognition

    The contribution was designated for recognising outstanding teachers. Local education representatives, teachers and company representatives attended the meeting.

    A continuing education programme

    The company established its student assistance foundation in 2004. Its education work includes student grants, support for teachers and local community programmes.

    View photographs from the education meeting

    Find equipment information

    Use the product catalogue to identify a crane type, or contact the team with your lifting task and site dimensions.

  • Heavy-Duty Cranes Support Tunnelling Equipment Manufacturing and Coal Research

    Heavy-Duty Cranes Support Tunnelling Equipment Manufacturing and Coal Research

    Project Deliveries

    Heavy-Duty Cranes Support Tunnelling Equipment Manufacturing and Coal Research

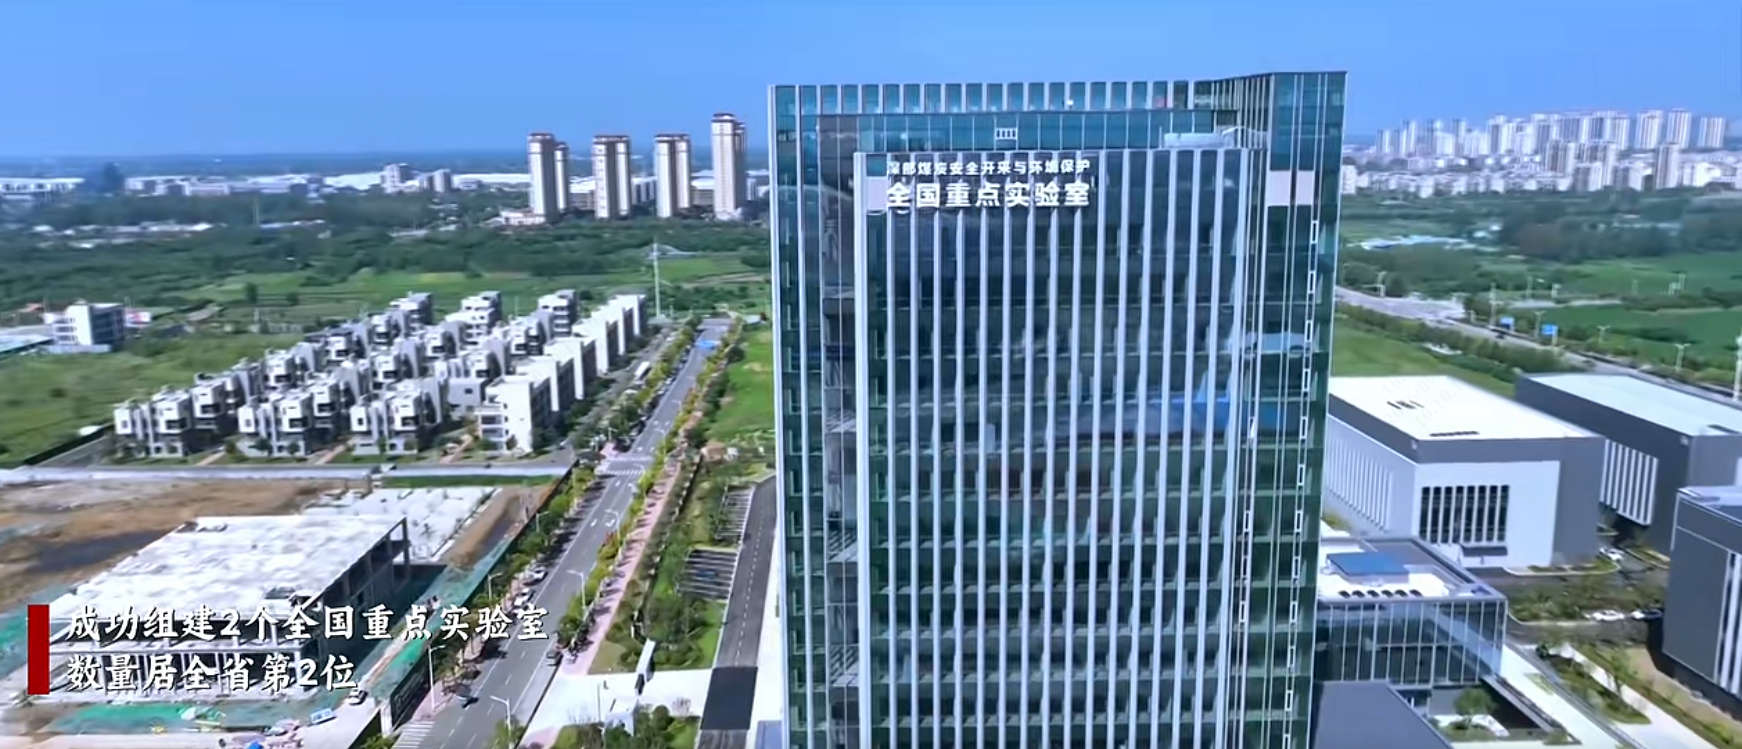
    Henan Mine Crane equipment has supported tunnelling machinery manufacturing and a national coal research facility, illustrating two distinct heavy-load applications.

    Yellow double-girder crane installed in an industrial building
    Yellow double-girder crane installed in an industrial building.

    Crane equipment for tunnelling machinery production

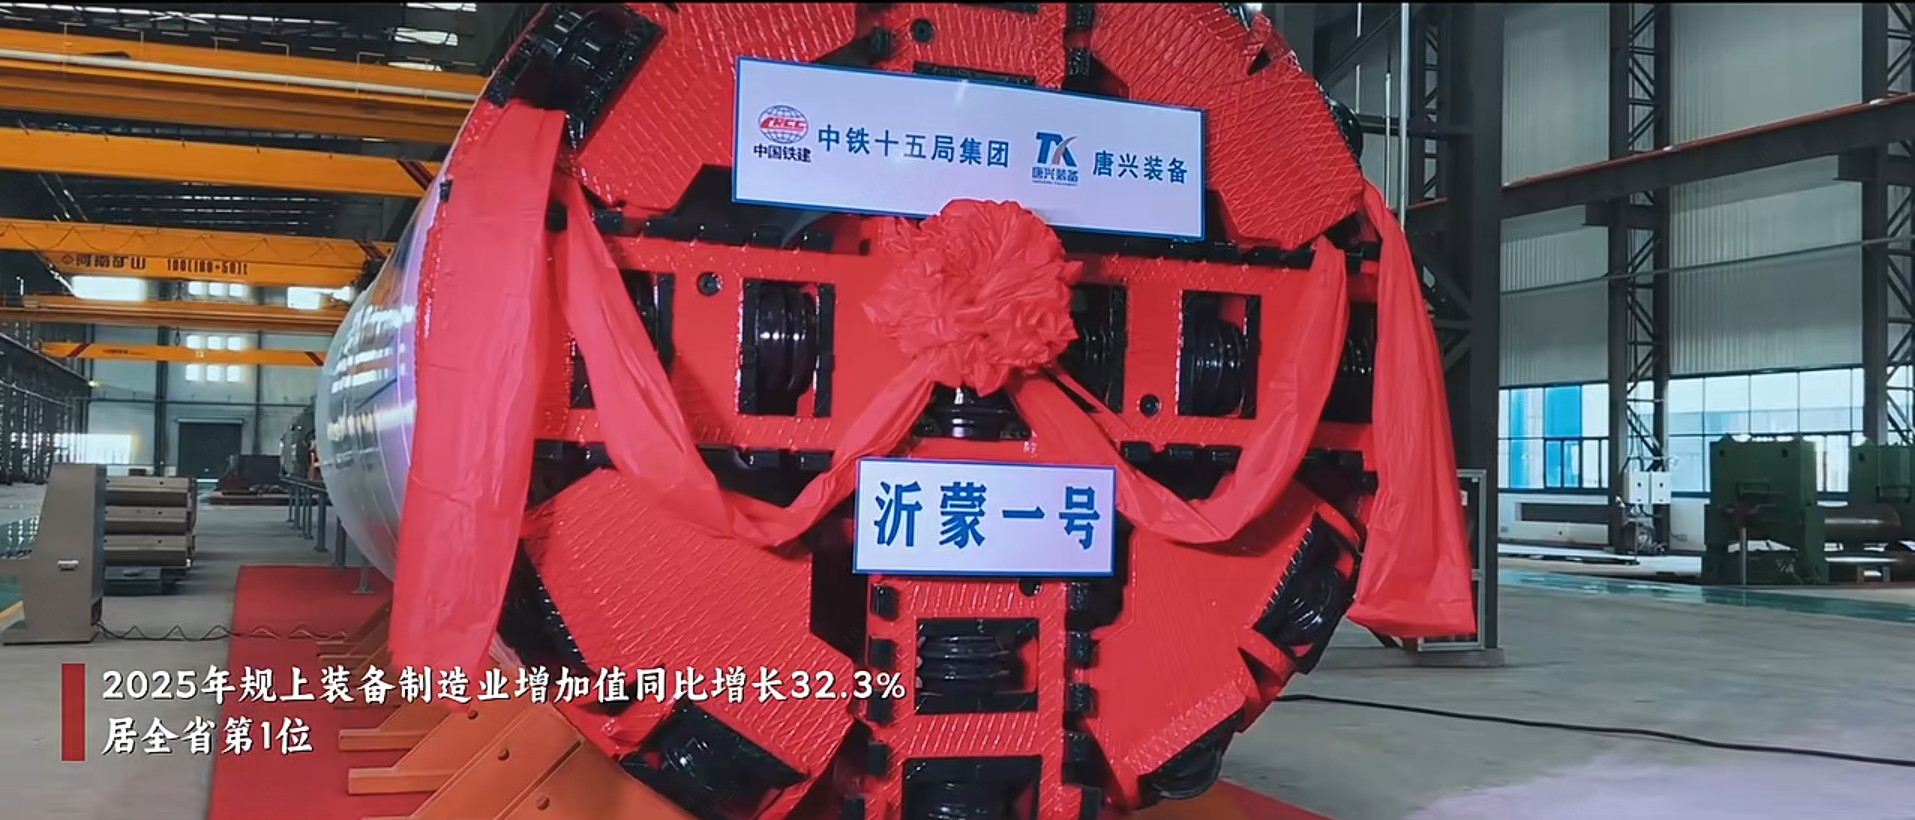
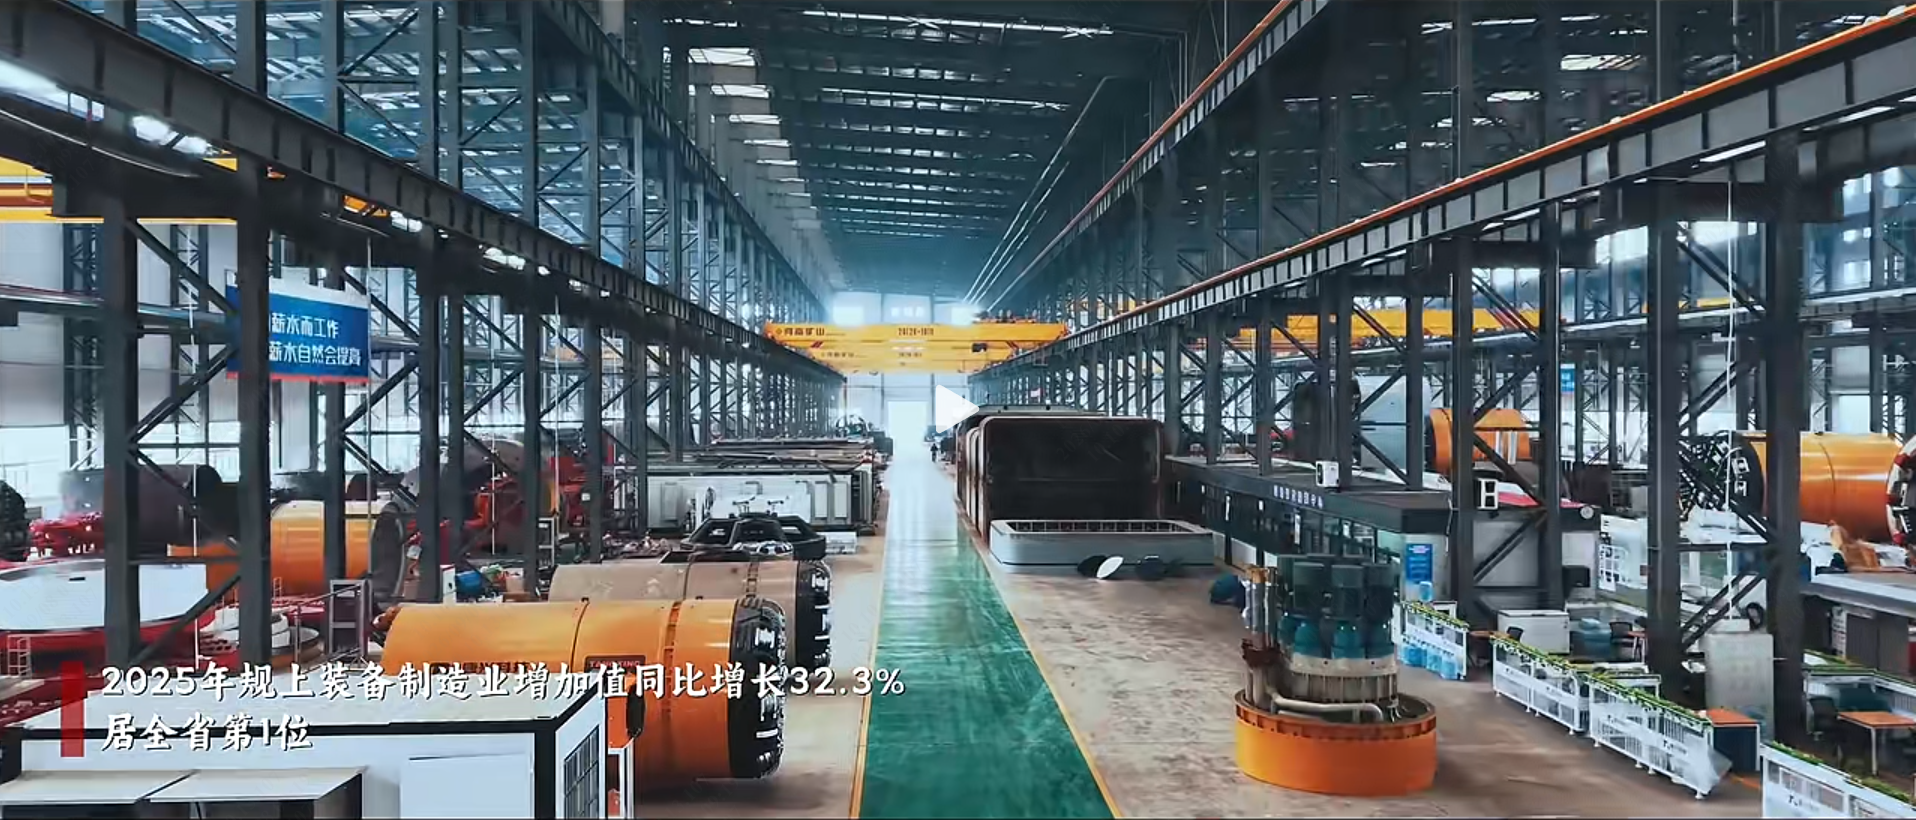
    More than 100 crane units were developed and manufactured for Tangxing Equipment’s trenchless equipment industrial park. The lifting equipment supported the manufacturing site associated with the rollout of the Yimeng No. 1 tunnel boring machine.

    Three 100 t cranes for research operations

    A separate application used three 100 t double-girder cranes at a national laboratory working on deep-coal mining safety and environmental protection. These are individual crane capacities, distinct from the number of units supplied to the manufacturing park.

    Plan heavy-component handling

    Provide the heaviest component, lifting points, required hook travel and building layout. Include any tandem-lifting or assembly-position requirements.

  • Henan Mine Crane Restarts Production After the Lunar New Year Holiday
    Henan Mine Crane Restarts Production After the Lunar New Year Holiday
    Company & People

    Henan Mine Crane Restarts Production After the Lunar New Year Holiday
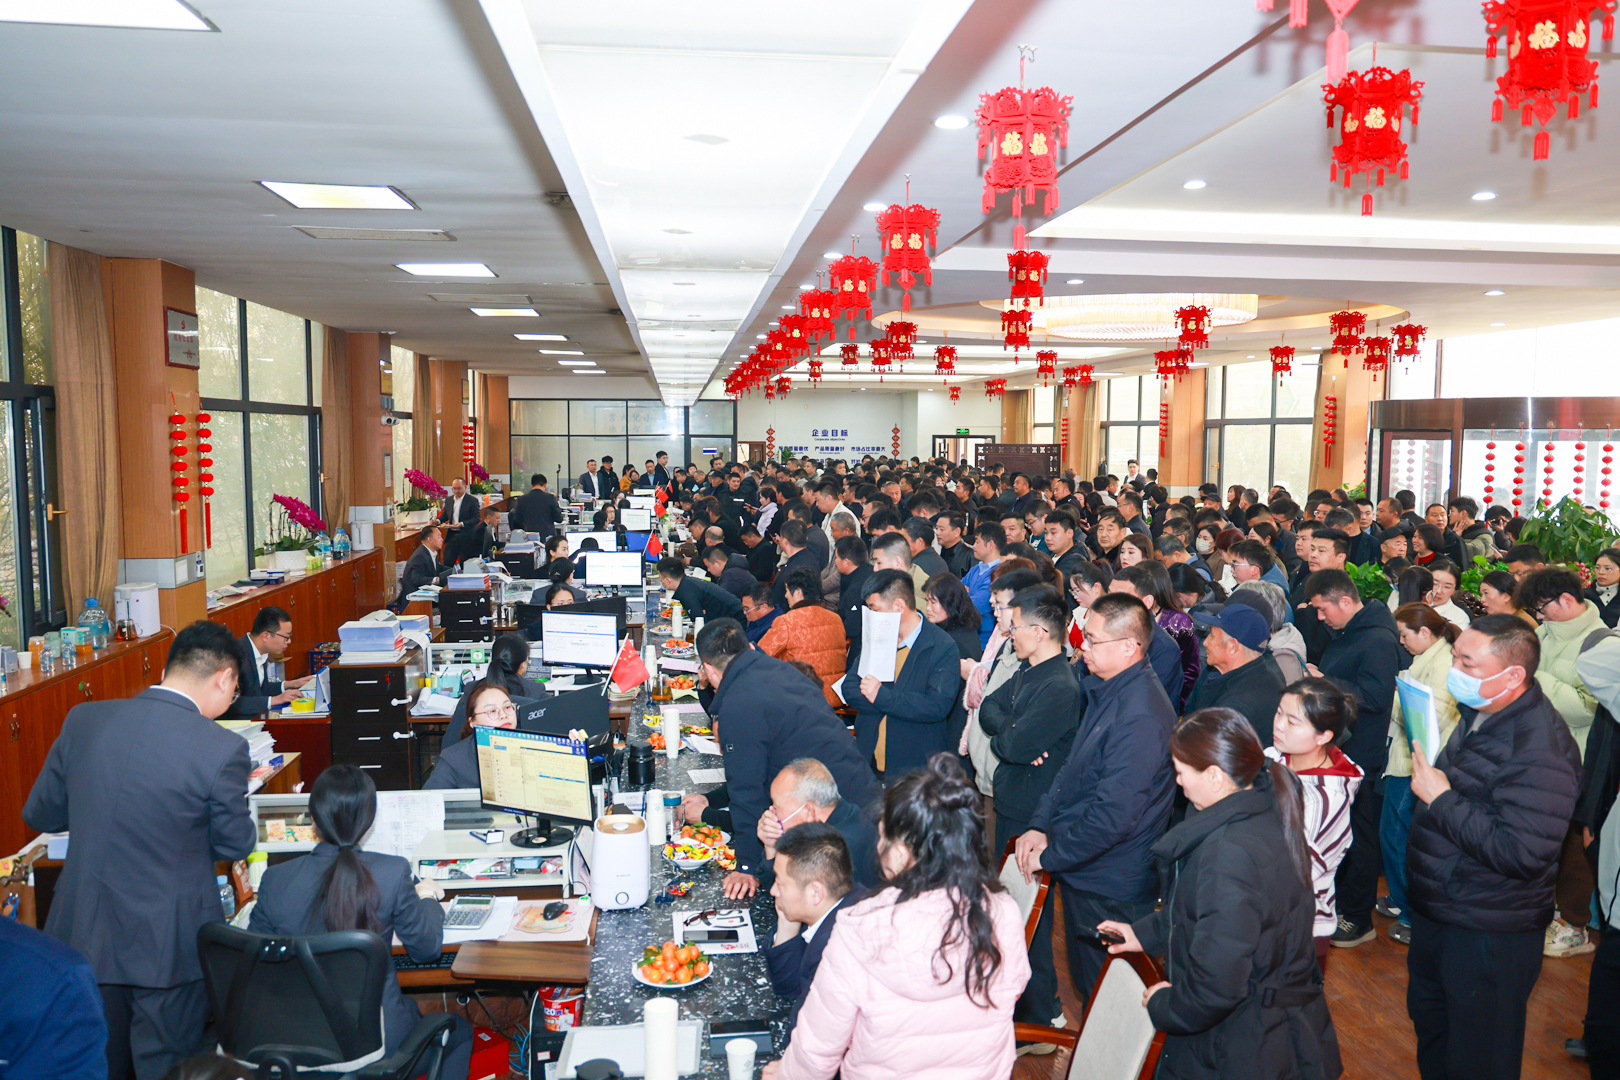
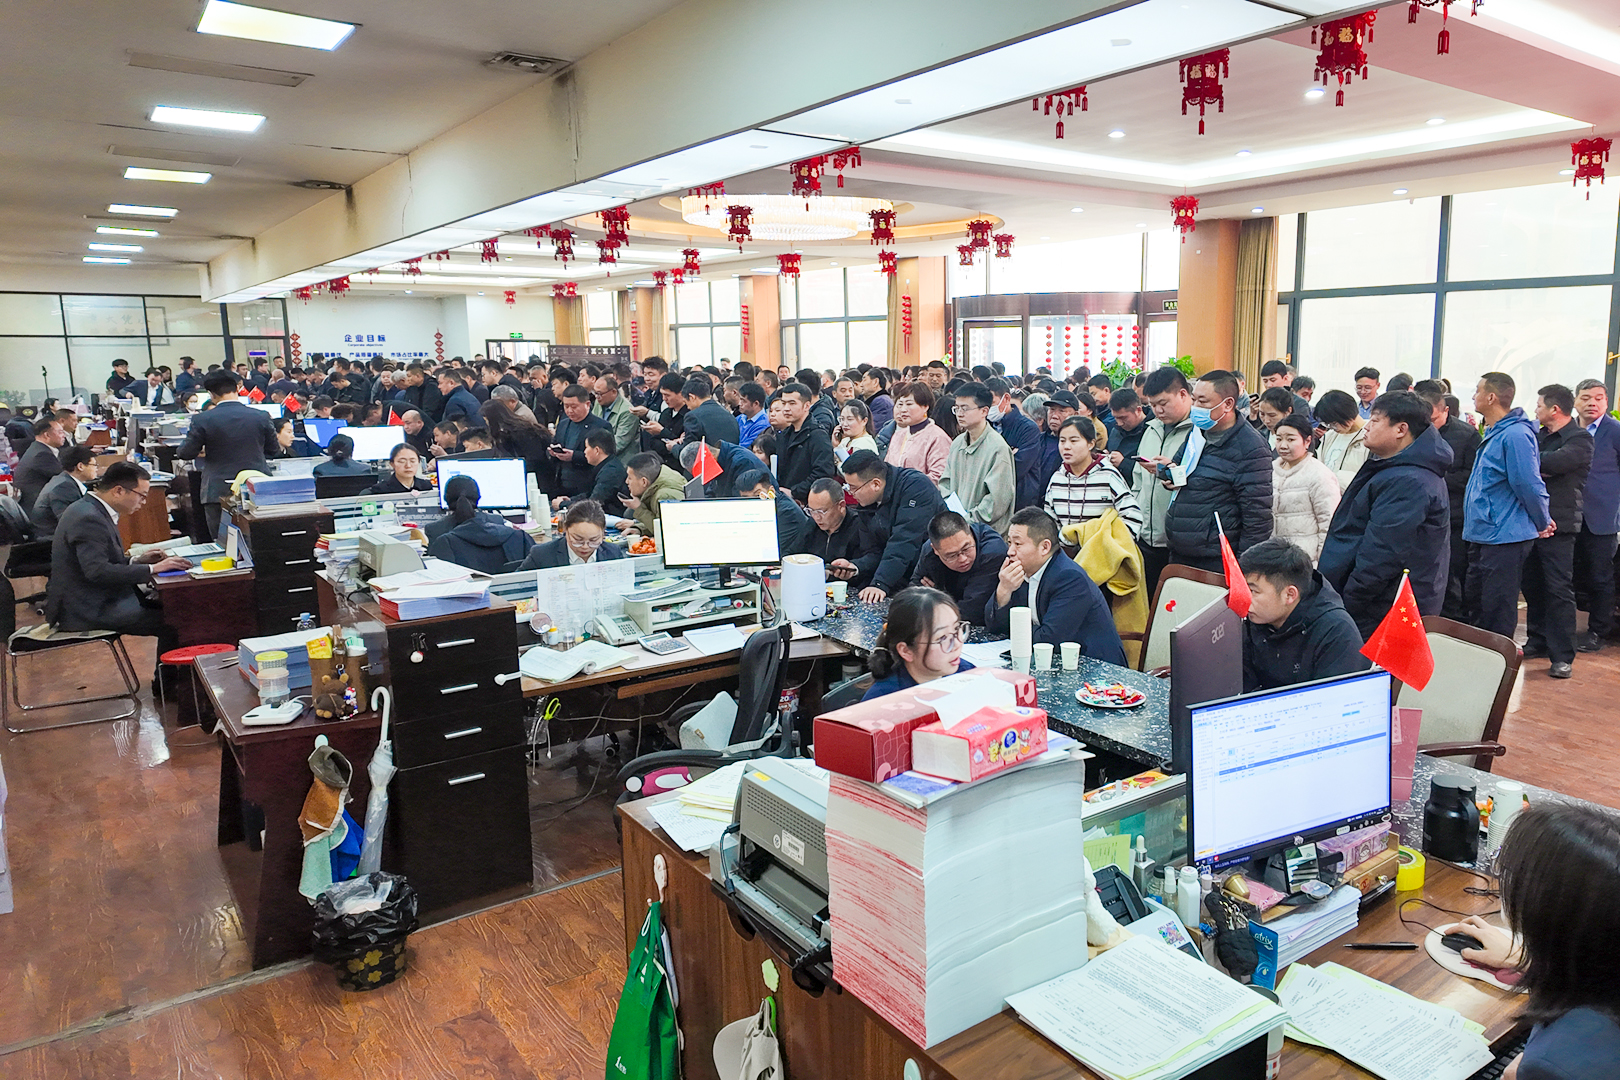
    Henan Mine Crane resumed work on 22 February 2026 after the Lunar New Year holiday. A three-day customer programme concluded on 24 February.

    Customer discussions in an office after the Lunar New Year restart
    Customer discussions in an office after the Lunar New Year restart.

    Workshop activity resumes

    The report describes production teams and robotic lines returning to work as the company resumed order-related manufacturing. New double-girder overhead cranes and intelligent crane equipment featured in the customer discussions.

    Confirm the schedule for your own order

    An individual project schedule depends on specification approval, manufacturing scope, inspection requirements and delivery responsibilities. Customers planning a purchase can send these details for a project-specific discussion.

    Contact Henan Mine Crane

    For product information, a manufacturing visit or a company enquiry, send the relevant details to our team.

  • Wire-Rope Hoist Training Connects Design Decisions with Workshop Practice

    Wire-Rope Hoist Training Connects Design Decisions with Workshop Practice

    Quality & Manufacturing

    Wire-Rope Hoist Training Connects Design Decisions with Workshop Practice

    Henan Mine Crane held training on European-style wire-rope electric hoist design and manufacturing on 11 February 2026 at its intelligent industrial park.
    Wire-rope hoist training session in the company lecture room
    Wire-rope hoist training session in the company lecture room.

    Design and manufacturing teams attend together

    Technical specialist Zhao Dingyuan delivered the session. Participants included hoist designers, workshop employees and technical staff from machining, quality assurance and production.

    Connecting the specification with manufacturing checks

    The training addressed the technical knowledge needed by teams involved in hoist development and manufacture. For a hoist purchase, load, lifting height, speed, working duty, power supply and installation conditions should be defined together.

    The equipment proposal and agreed inspection records provide the project-specific basis for reviewing the selected hoist.

    Discuss your lifting requirement

    Provide the load, lift height, speed, duty and installation drawing for a hoist selection discussion.