Bridge Crane Problems: Record Symptoms and Plan a Technical Assessment
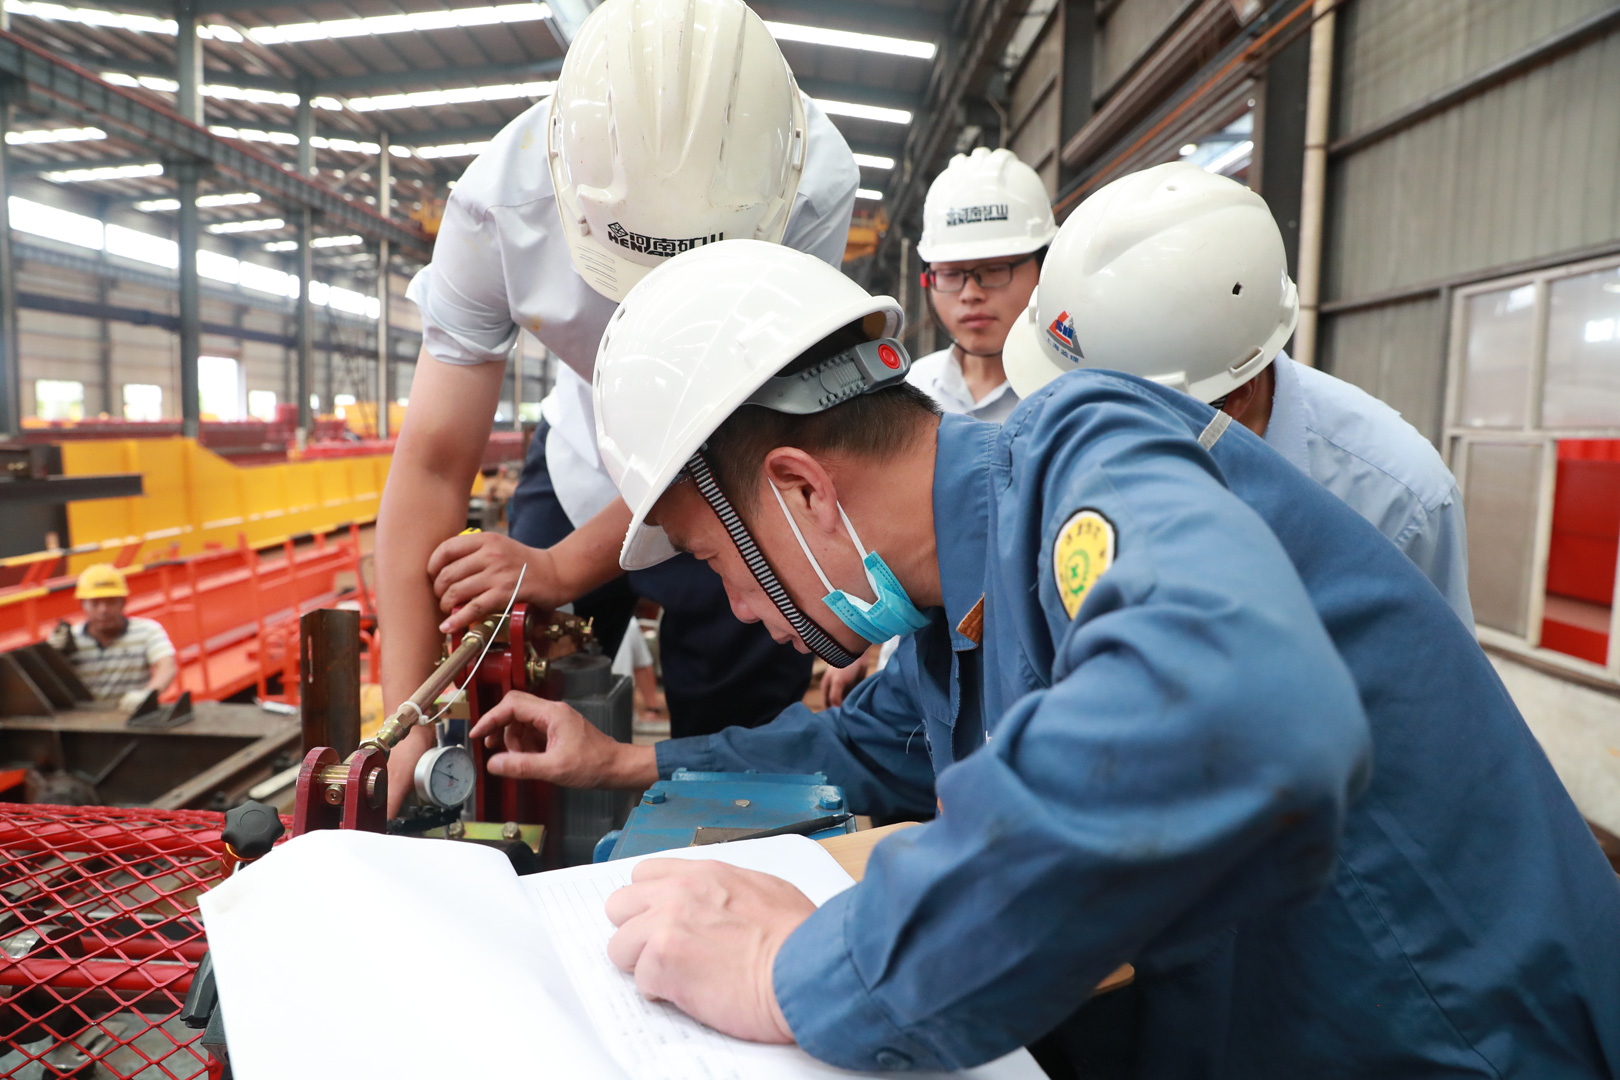
Repeated faults need evidence about when and where they occur. Organise the symptoms, operating conditions and inspection records so qualified service teams can assess the connected equipment instead of treating each symptom in isolation.
Key points for this crane project.
- What Is a Bridge Crane?
- Why Bridge Crane Problems Matter for Safety and
- Wire Rope Damage and Wear
What Is a Bridge Crane?
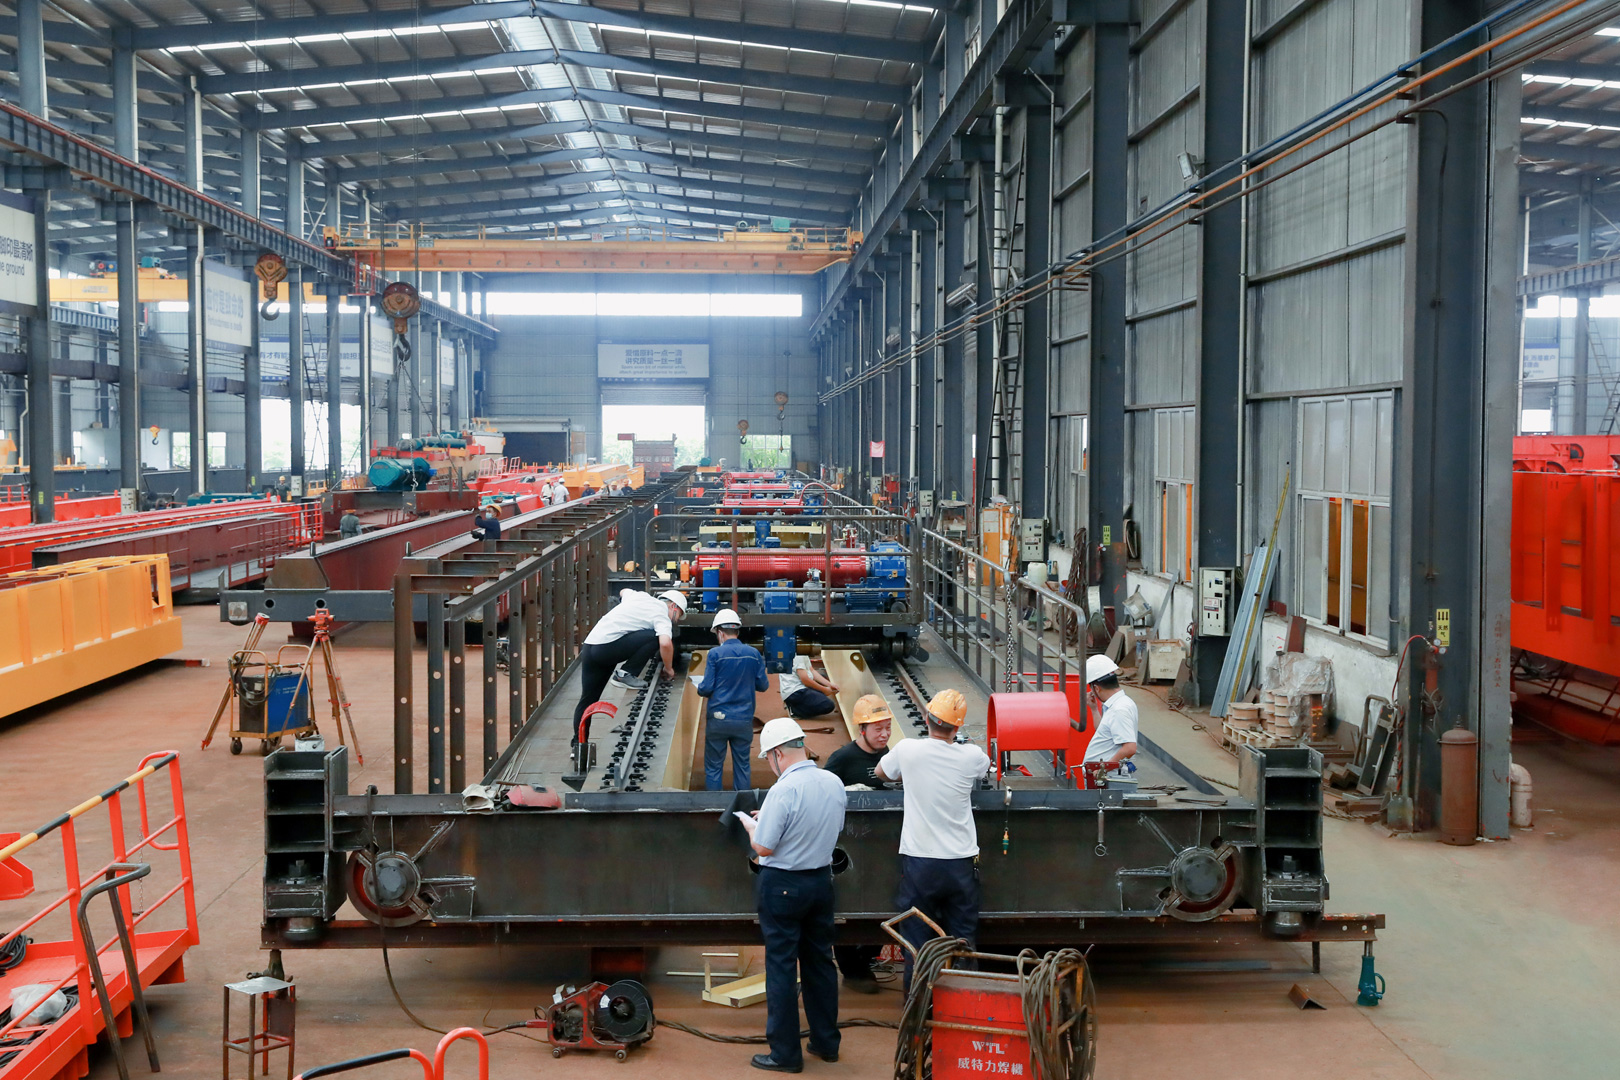
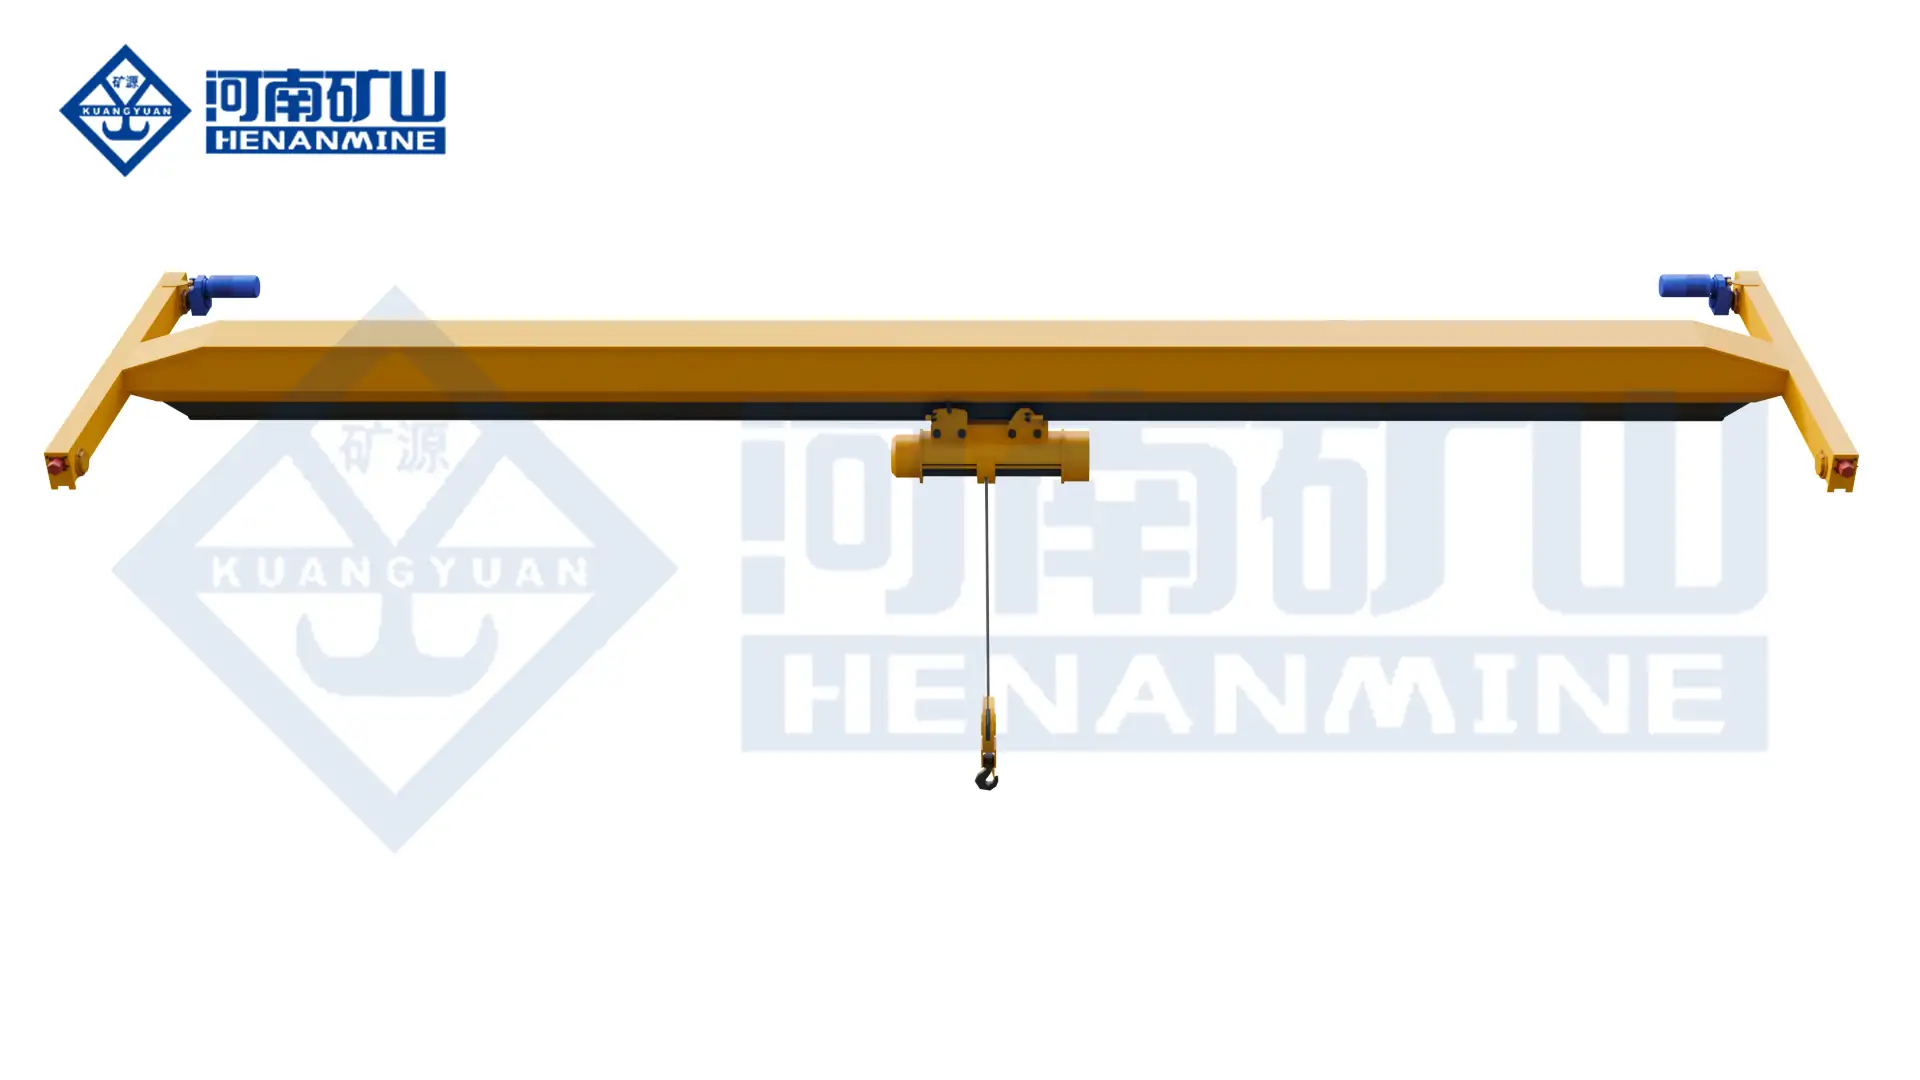
Henan Mine Crane bridge crane (also called an overhead crane) is a material handling machine that runs on elevated runway rails, lifting and moving loads along the length of a building using a bridge, trolley, and hoist. It works by combining a horizontal bridge girder that travels down the runway with a trolley that moves across the bridge, allowing the hoist to reach almost any point in the work envelope. It matters because it's often the single piece of equipment a facility depends on most to move heavy materials safely, efficiently, and repeatedly — which is exactly why unplanned downtime on a bridge crane is so costly.
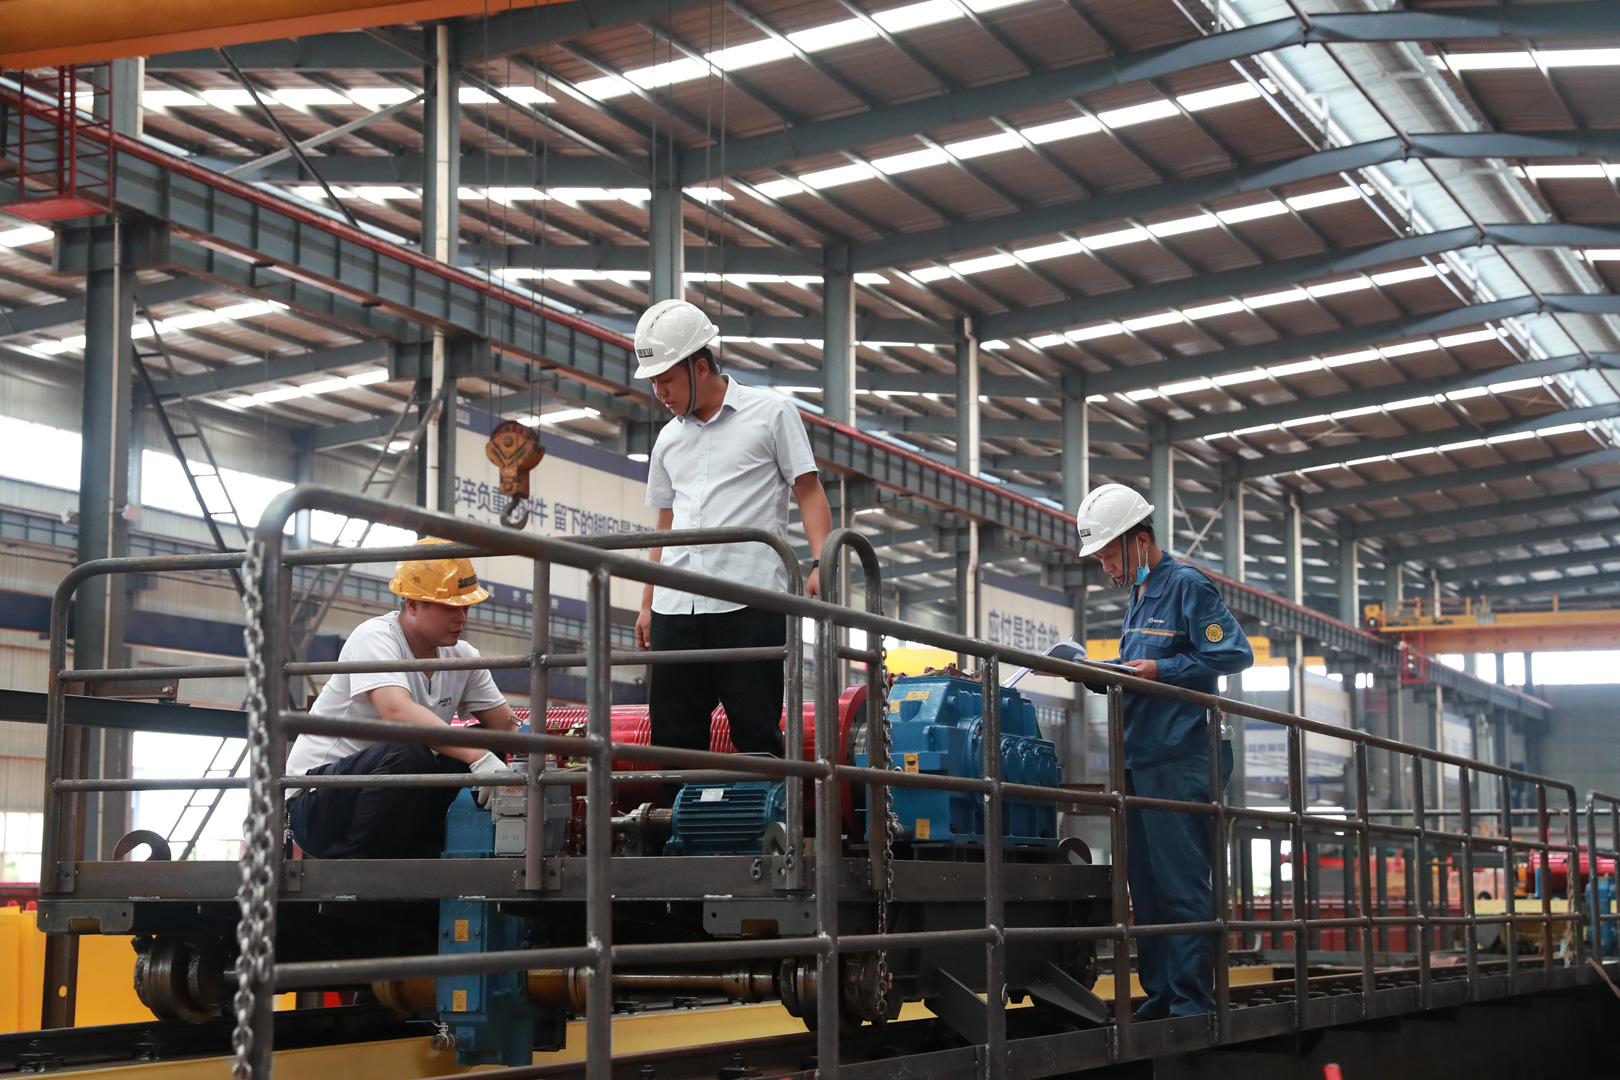
Bridge cranes are mechanically simple in concept but mechanically demanding in practice: every cycle puts stress on wire rope, brakes, wheels, and electrical contacts. Over thousands of cycles, that stress turns into the 10 problems below.
Why Bridge Crane Problems Matter for Safety and Compliance
Bridge crane failures aren't just a productivity issue — they're a regulatory and safety issue. OSHA 29 CFR 1910.179 requires documented daily, frequent (monthly), and periodic (annual) inspections of overhead and gantry cranes, and failure to maintain that documentation can result in fines on top of the cost of the breakdown itself.
The financial case is just as direct. Industry data on crane maintenance practices shows that a systematic, root-cause approach to troubleshooting — rather than reactive, trial-and-error repairs — meaningfully reduces average repair time and gets equipment back into service faster. Combined with the fact that most of the 10 problems below give early warning signs (noise, vibration, scraping, blown fuses), the takeaway is simple: catching a symptom early is always cheaper than replacing the component it was warning you about.
Wire Rope Damage and Wear
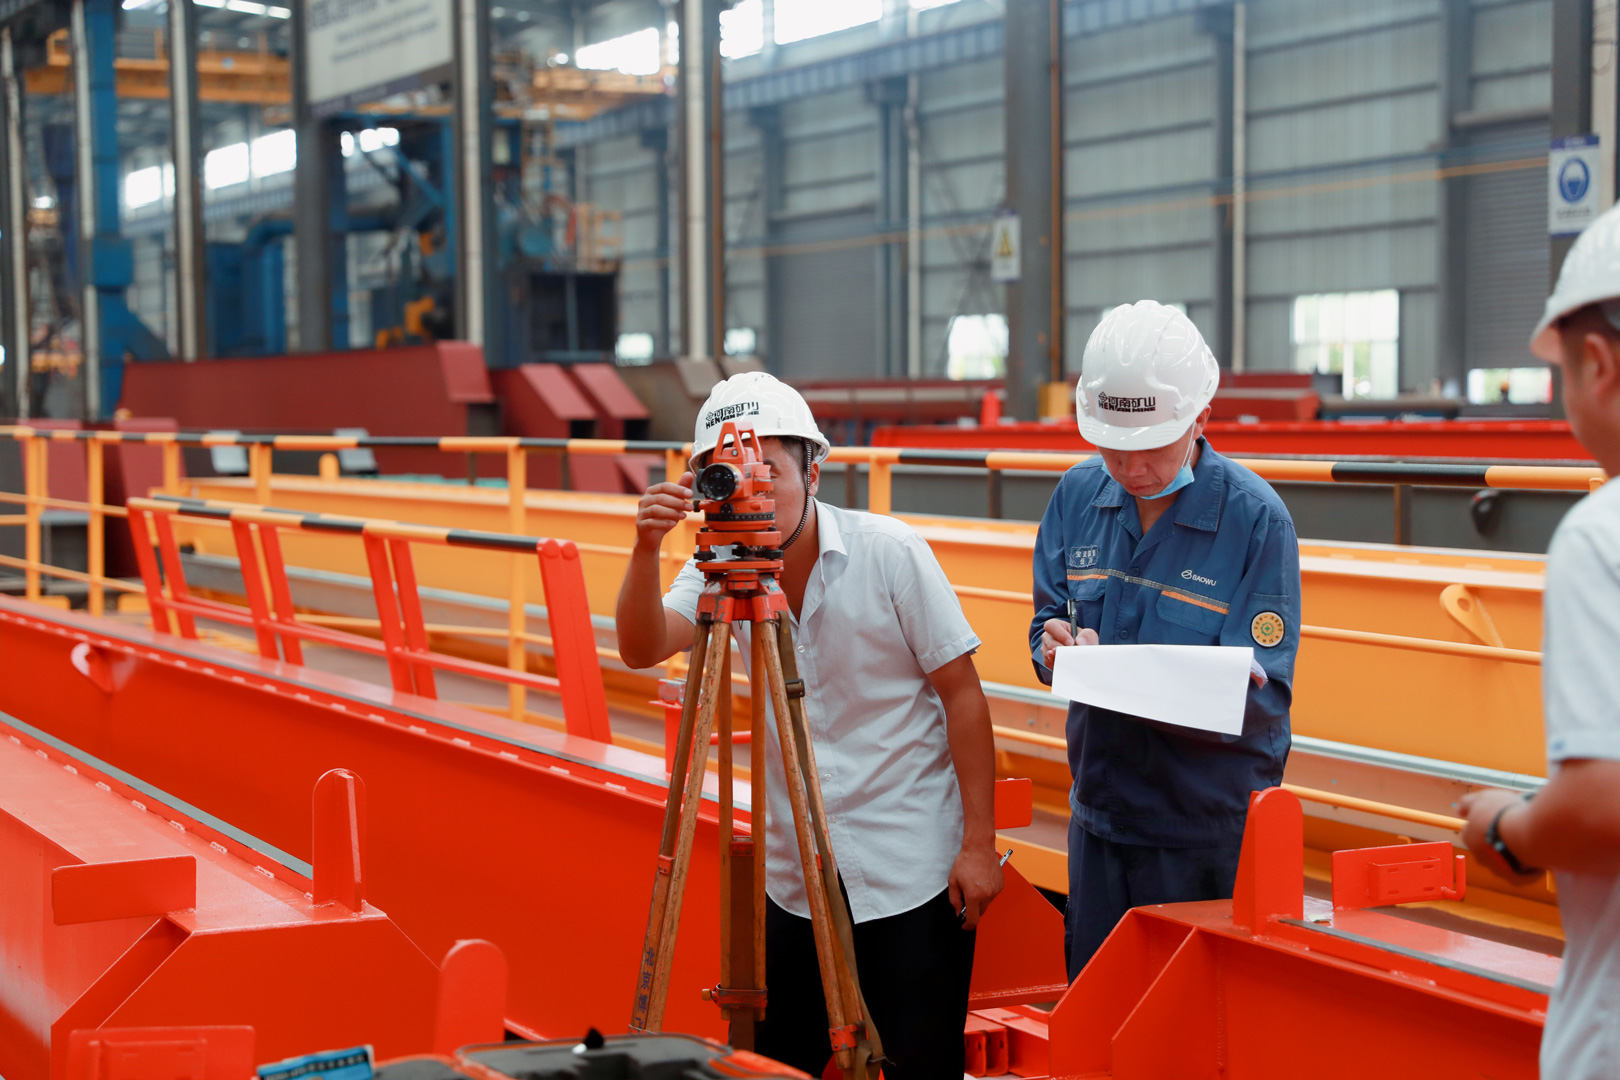
Signs: Obvious kinks, fractured or unravelled outer strands, flattened areas, rust or pitting, “bird caging”–outer strands rupture and separate with outward bulges.
Causes: Overloading, improper reeving, abraison against sheaves, corrosion due to moisture or chemicals or just plain fatigue from repeated lifting cycles.
Fix: Cease operation of the wire rope as soon as deterioration is observed, this should not be a “monitor and continue” situation. Replace wire rope with an OEM replacement of same specifications as crane for load rating and reeving.
Prevention: Daily examination of wire rope before each shift (use torch for inspection). Use lubrication guides from the importer. Never shock load the wire rope, or exceed the maximum crane capacity (damages four times faster than the duty cycle).
Bent or Cracked Hooks
Symptoms: Visible bending, throat opening wider than spec, cracks, or twisting of the hook body.
Causes: Overloading is the leading cause — hooks are engineered for a specific load rating, and exceeding it even occasionally can deform the metal permanently. Side-loading (lifting at an angle instead of straight up) is a close second.
Fix: A bent, cracked, or out-of-spec hook must be replaced, not reshaped or welded back into service. Hooks are a single point of failure for the entire load, so there's no safe field repair for structural deformation.
Prevention: Inspect hooks and below-the-hook devices at the start of each shift. Use load charts and rated capacity indicators so operators never have to guess whether a lift is within limits.
Brake Failure or Slippage
Symptoms: The load swings or creeps after the operator has released the control, the crane doesn’t stop smoothly, or an abnormal noise or delay occurs when the brake is applied.
Causes: Worn Brake Linings, Dirty or contaminated brake oil or grease, Incorrect brake torque or an electrical fault which prevents the brakes from applying or releasing.
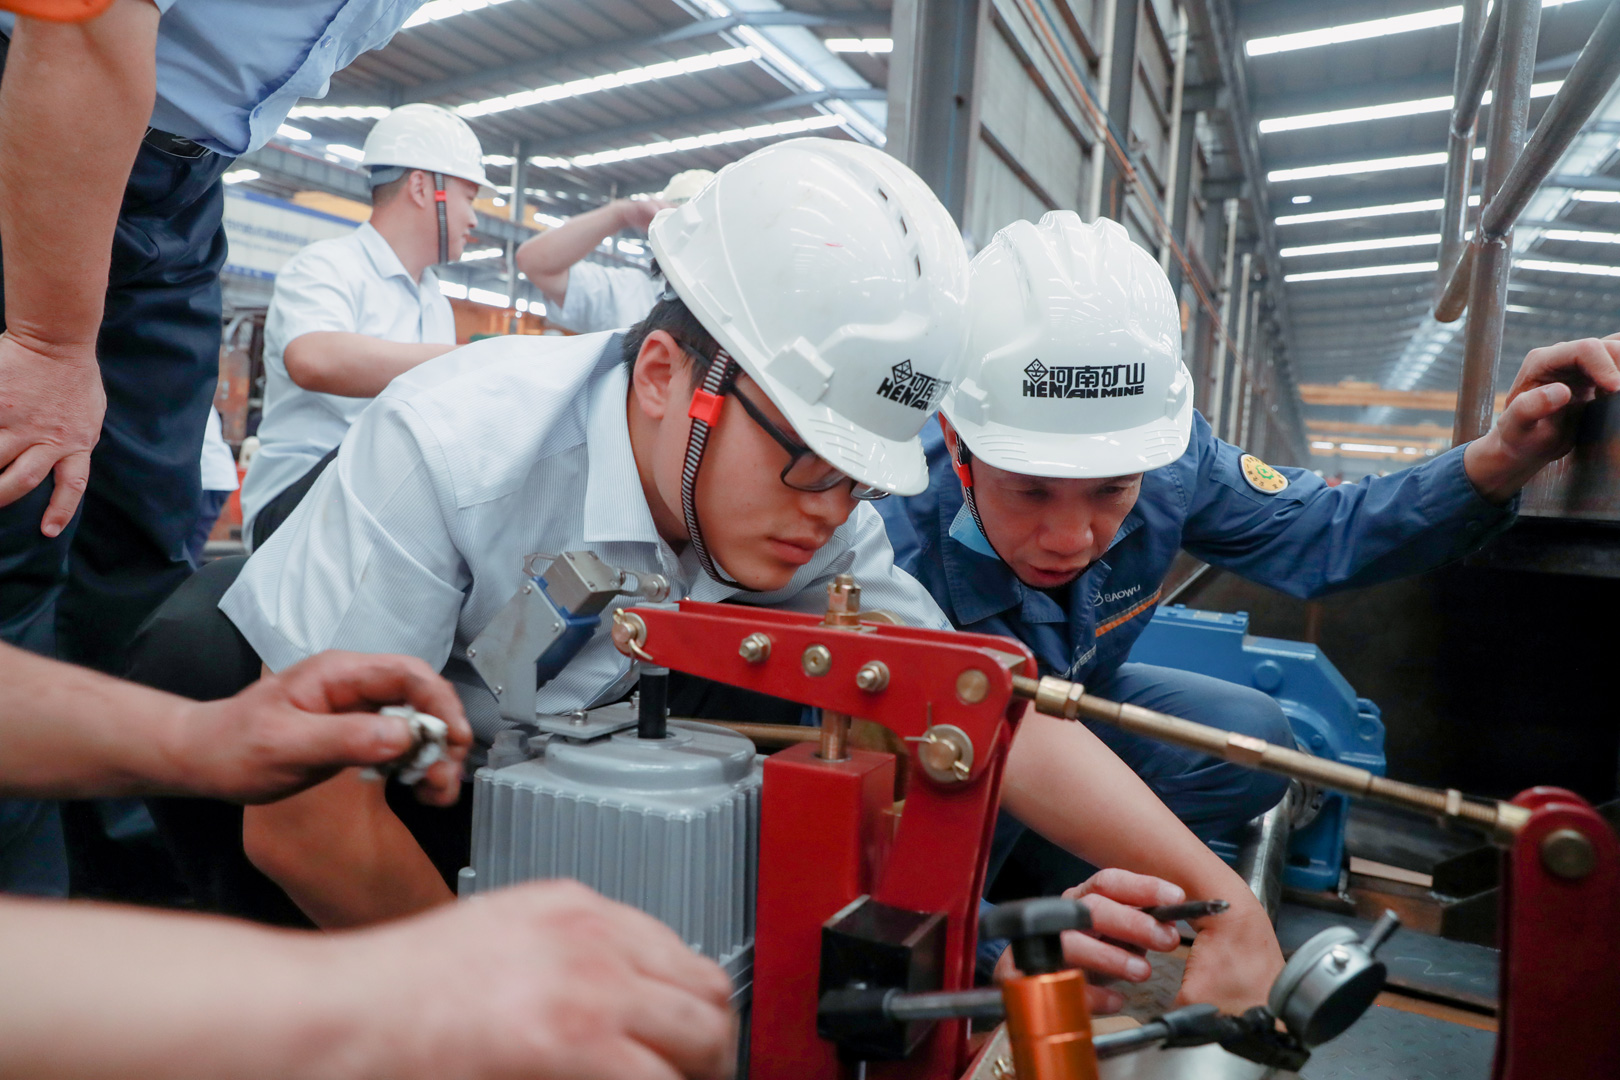
Fix: Change worn brake pad or lining, clean contaminated components,adjust brake torque to manufacturer‘s specification. If a brake does not grip and maintain a load suspended by the crane this is a stop-work problem – the crane must not be operated until it has been rectified.
Prevention: Check brake response as part of the operational check at each shift change. Check annually for the kind of brake inspections that are part of the monthly preventive maintenance, since linings wear in a steady, predictable fashion.
End Truck Wheel Wear and Misalignment
Signs: Irregular wheel tread wear; a scraping or grinding noise when moving; a power shift crawler which needs more than usual effort to have it rolling.
Causes: Continued wear from recurring years of travel, unequipped wheel hardness relative to rail hardness, or inherent skew/tracking issues leading to applying uneven stresses on the wheel.
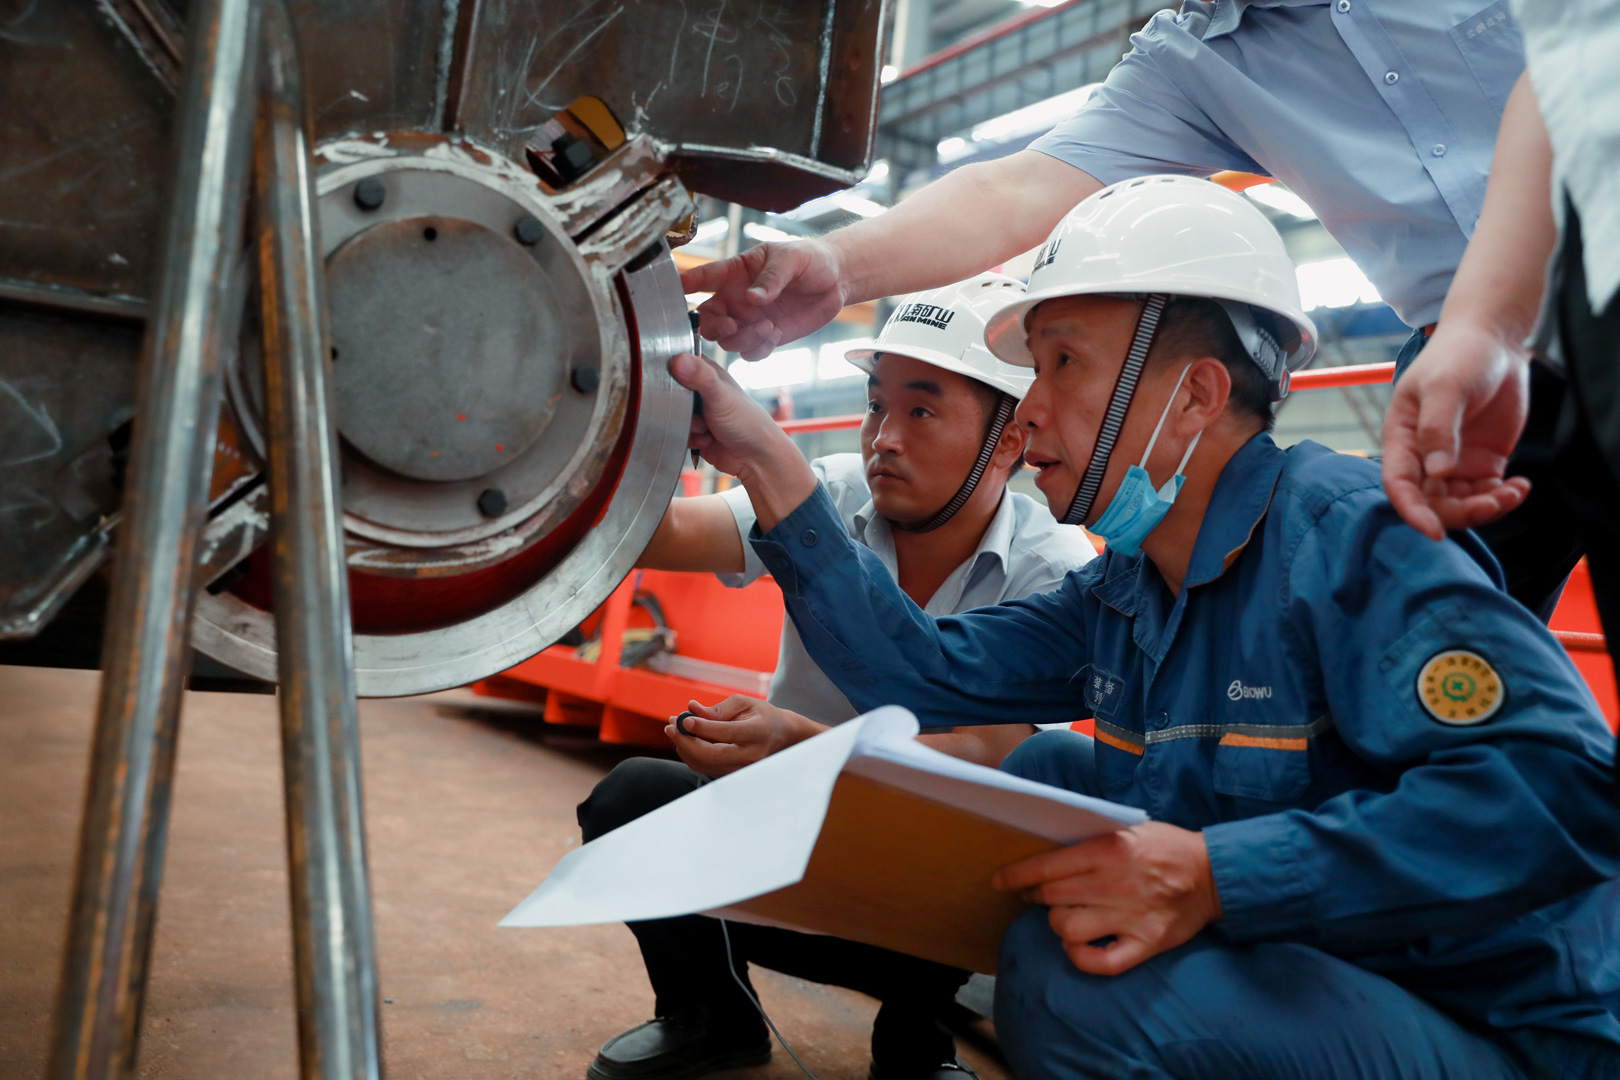
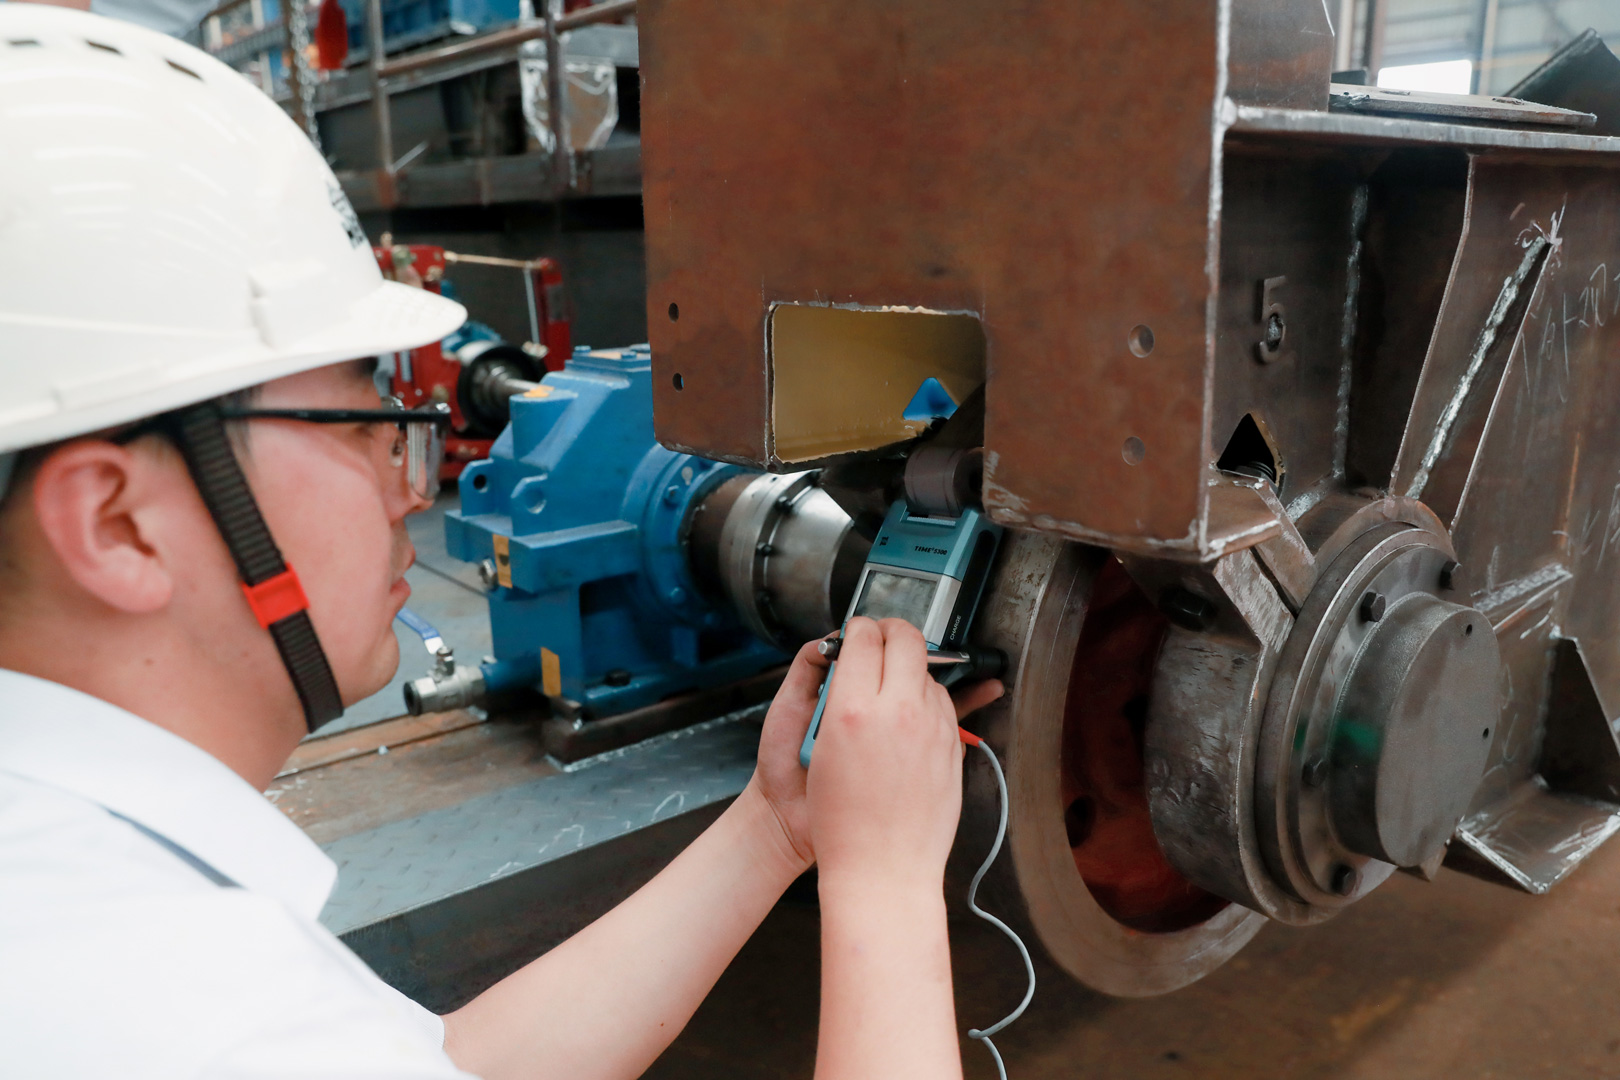
Wheel repair: Swap out worn wheels with OEM equivalent (should match existing wheel hardness for the rail material). If wheels are wearing irregularly side to side then explore tracking adjustment options for correction prior to replacing the wheels otherwise the new wheels are going to wear just as quickly.
Prevention: Inspect wheel treads as part of your scheduled monthly maintenance. Maintain clean runway rails and gutters. Dirt and debris can accelerate wheel wear and hide early symptoms of misalignment.
Crane Skewing and Runway Tracking Issues
Signs: The crane “crabs” or angles slightly as it moves, makes a grinding/scraping noise at the end trucks when running or pushes harder against one rail than the other.
Causes: Skewing occurs when traction variations between the left and right drive wheels results in a slight rotation of the bridge out of perfect right angle to the runway. This eventually deteriorates into a skew if present wheel/rail wear, misalignment of the runway rails, or uneven performance of drive motors side-to-side.
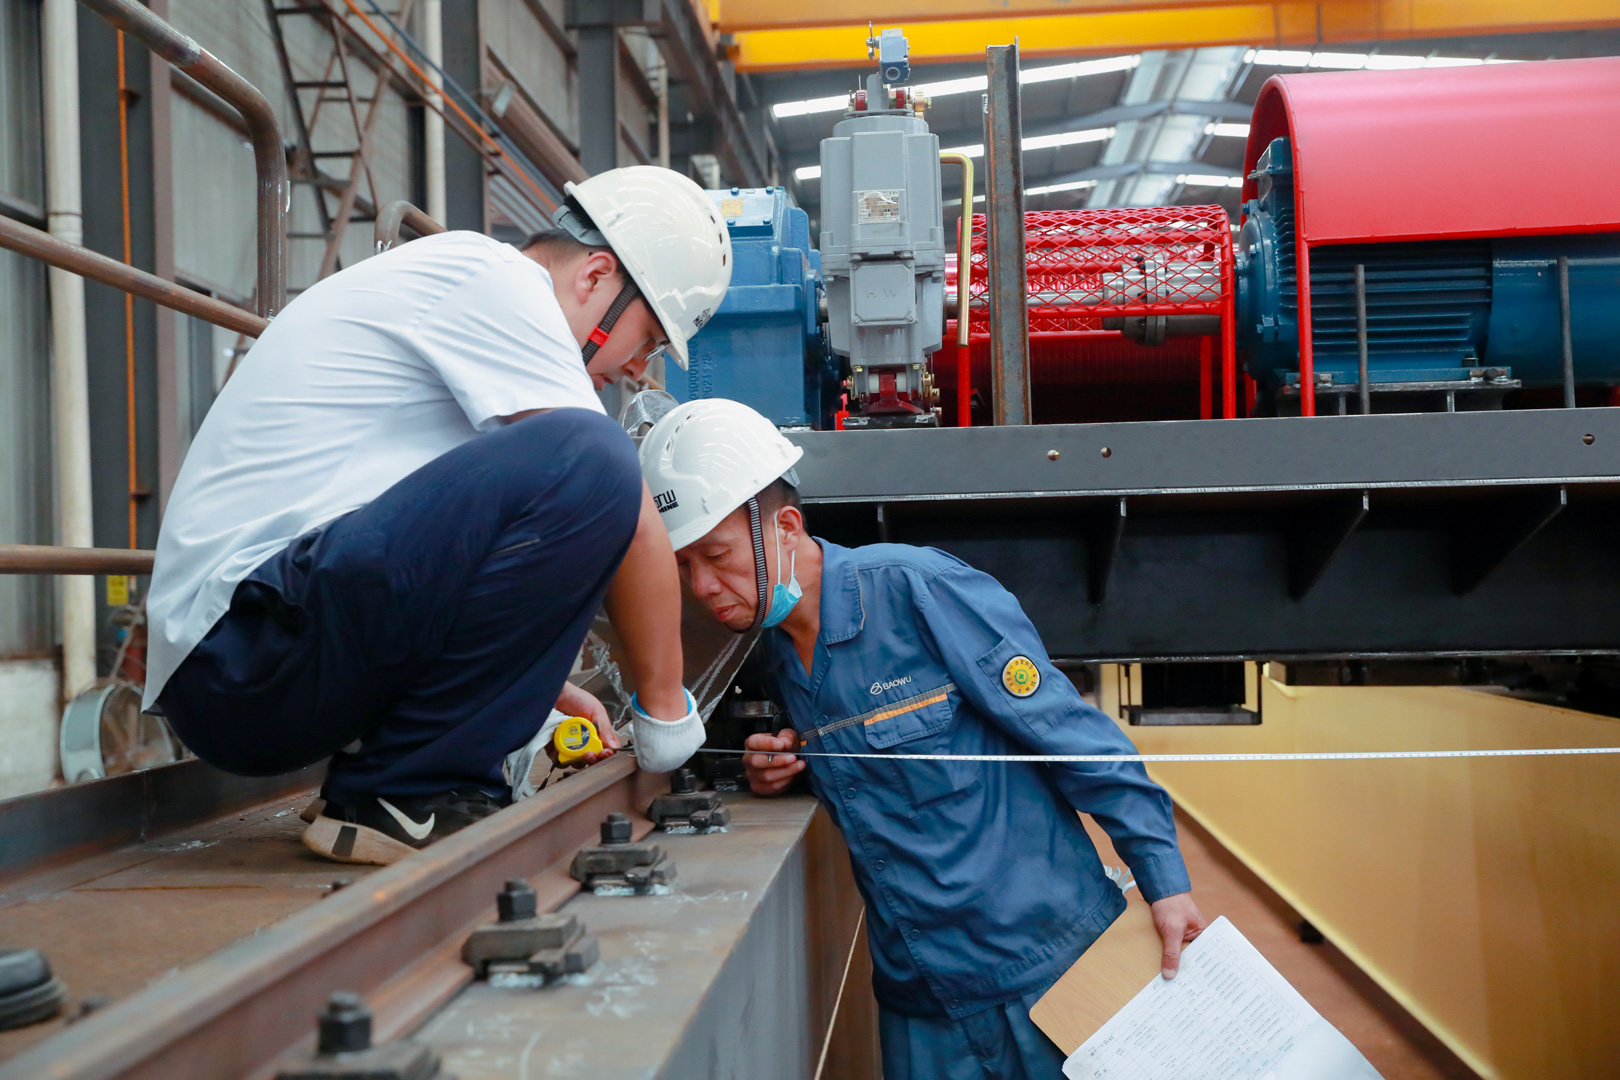
Fix: An ongoing problem with the skew will need a Runway Alignment Inspection and will not simply need a wheel change. The root cause can be discovered with a trained crane technician measuring run way gauge, rail elevation and end truck alignment.
Prevention: Do not fall into the trap of forcing squareness by “slamming” the crane against the end stops. This can be very harmful to the structure. Regular runway squareness testing should be done at regular intervals. This is especially critical on older or heavily traveled systems.
Electrical Faults: Blown Fuses and Conductor Bar Problems
Symptoms: Frequent blowing of fuses, intermittent power loss to crane, or poor control response.
Causes: Blowing fuses too often is almost certainly a circuit fault rather than coincidence. Most cases are caused by oxidized or worn contactor components, poor connection between the conductor bar and collector, loose connections in power or junction boxes, or motor winding faults causing excessive current draw.
Fix: Don’t simply replace the fuse and continue operating — this only addresses the symptom, not the root cause. Arrange for the electrical system to be tested and the fault identified. Conductor bar condition should be checked. Collector contact pressure should be inspected, and any corrosion or loose connections must be repaired.
Prevention: Check conductor bars and collectors on a monthly basis. Ensure electrical boxes are properly sealed to prevent the ingress of dust or water, which are the main causes of oxidation and poor contact.
Pendant or Radio Control Failures
Symptoms: The crane is unresponsive to commands / has a delay of response / moves in a jerking motion instead of smooth control.
Causes: For radio controls the favorite culprits are an empty/dead transmitter battery, loss of sight to the receiver, or interference from other equipment. For pendant controls it is usually an open or severed cable conductor.
Fix: First try just the basics, change or charge the battery in the transmitter, make sure it has a clear line of sight to the receiver, and power-cycle (reboot) the transmitter. If it still isn’t working, the fault is most likely in the receiver inside the pendant wiring, and you need to call a technician.
Prevention: Always repair a safety interlock or other control system that is not functioning do not just ignore a monitor and “keep working.” This is one of the leading causes of “minor” problems resulting in serious accidents. Make battery and cable checks part of the normal maintenance.
Motor Overheating and Failure
Symptoms: Excessively hot motor housing, decreased raising or traveling speed, abnormal noise or the motor repeatedly tripping out its overload.
Causes: Excessive loading of crane. Running the crane over rated capacity. Operating the crane too rapidly, that is starting and stopping more frequently than allowed with insufficient time to cool, unbalanced three phase supply voltage, worn bearings and windings from age and service it has received.
Solution: Be sure to let the motor cool down and check the load and duty cycle which was happening just before the motor overheated. If the motor overheats again with no obvious load problem then the motor’s windings and bearings should be tested and check the three phase voltages as imbalanced voltages is a very typical but often missed reason for the stress to the motor.
Prevention: Use motor overheating protectors and takeover requirements into account, don’t operate the crane perpetually above its class rating. Clean motors and inspect them monthly.
Gearbox, Coupling, and Abnormal Noise or Vibration
Symptoms: Grinding, knocking or whining noise while running; shaking or vibration while traveling or lifting; or apparent oil leakage from gearbox seals.
Causes: Worn gears from age and duty cycle, low or contaminated lubricant, misaligned couplings or loose mounting bolts, permitting parts to move under load.
Fix: For oil leaks, replace worn seals and bolt up the housing firmly. If the gearbox is making a lot of noise or vibrating, check gear teeth and coupling alignment; while it may seem easier at the time to run the crane with gearbox damage, this will lead to an immediate, more costly breakdown.
Prevention: Adhere to the manufacturer’s lubrication schedule carefully, as both lack of and excess of lubrication can speed up gear wear. Monitor any new or changing noise as a maintenance item rather than a reason to continue operating.
Limit Switch Malfunctions and Hoist Over-Travel
Symptoms: The hoist doesn’t stop at end of travel, the travel limits activate prematurely or irregularly, or the crane keeps moving after the operator releases the control close to a limit.
Possible causes: A worn or defective limit switch, a switch blocked by debris, a wiring fault interrupting the switch signal to the control system.
Fix: During regular inspection all limit switches should be tested and any that do not activate reliably should be reset or replaced. Over-travel is a major safety risk; malfunction of a limit switch on the upper travel end of a hoist could lead to equipment damage or to loads slipping.
Prevention: Include limit switch testing in each pre-operational shift check, rather than periodic maintenance, since it is one of the few failure modes where the result (over-travel) can occur on the very next lift.
Discuss the crane arrangement for your project.
Repeated faults need evidence about when and where they occur. Organise the symptoms, operating conditions and inspection records so qualified service teams can assess the connected equipment instead of treating each symptom in isolation. Share the load, available drawings, working cycle and site conditions with Henan Mine Crane so the required configuration and supply boundary can be discussed.
Related crane configurations
Single-Girder Bridge Crane
View product parametersUse an LDA single-girder bridge and electric hoist for general workshop material handling. Select the lifting capacity, runway geometry and hoist duty around the building and load.
LH Electric Hoist Double Girder Crane
View product parametersUse an LH double-girder bridge with an electric-hoist trolley for workshop lifting, assembly and maintenance. Match the hoist arrangement to the suspended load, hook travel and available building space.
Updated 2026 · Henan Mine Crane