博客

  • Bridge Crane for Precast Concrete Factory

    Bridge Crane for Precast Concrete Factory

    Bridge Crane for Precast Concrete Factory

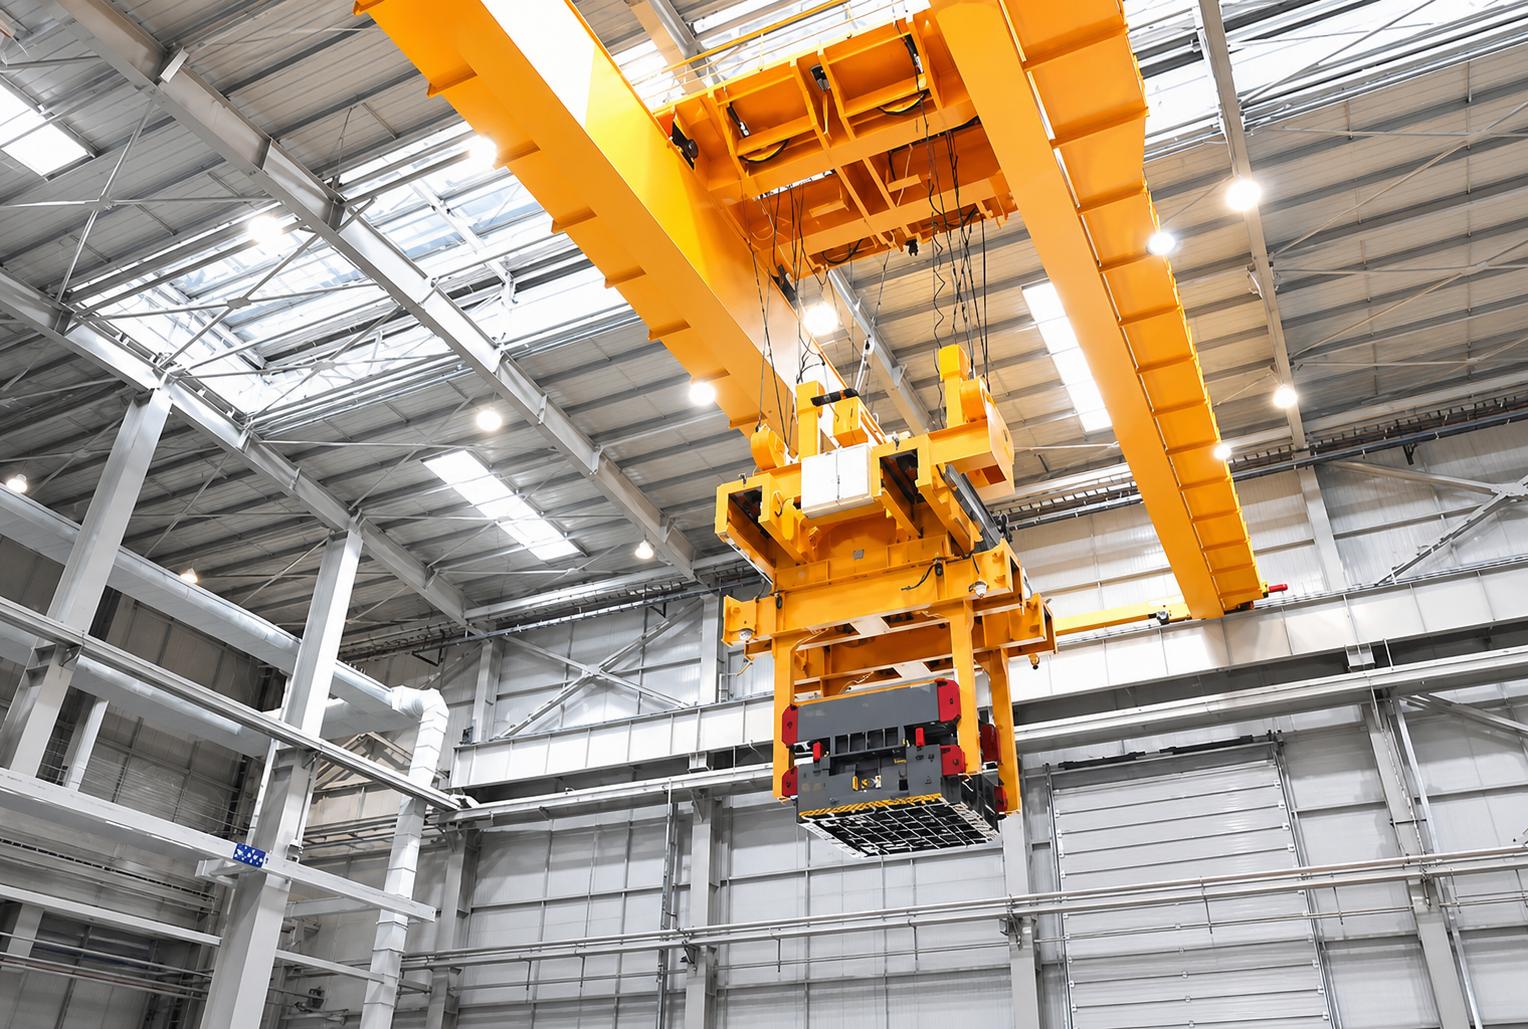
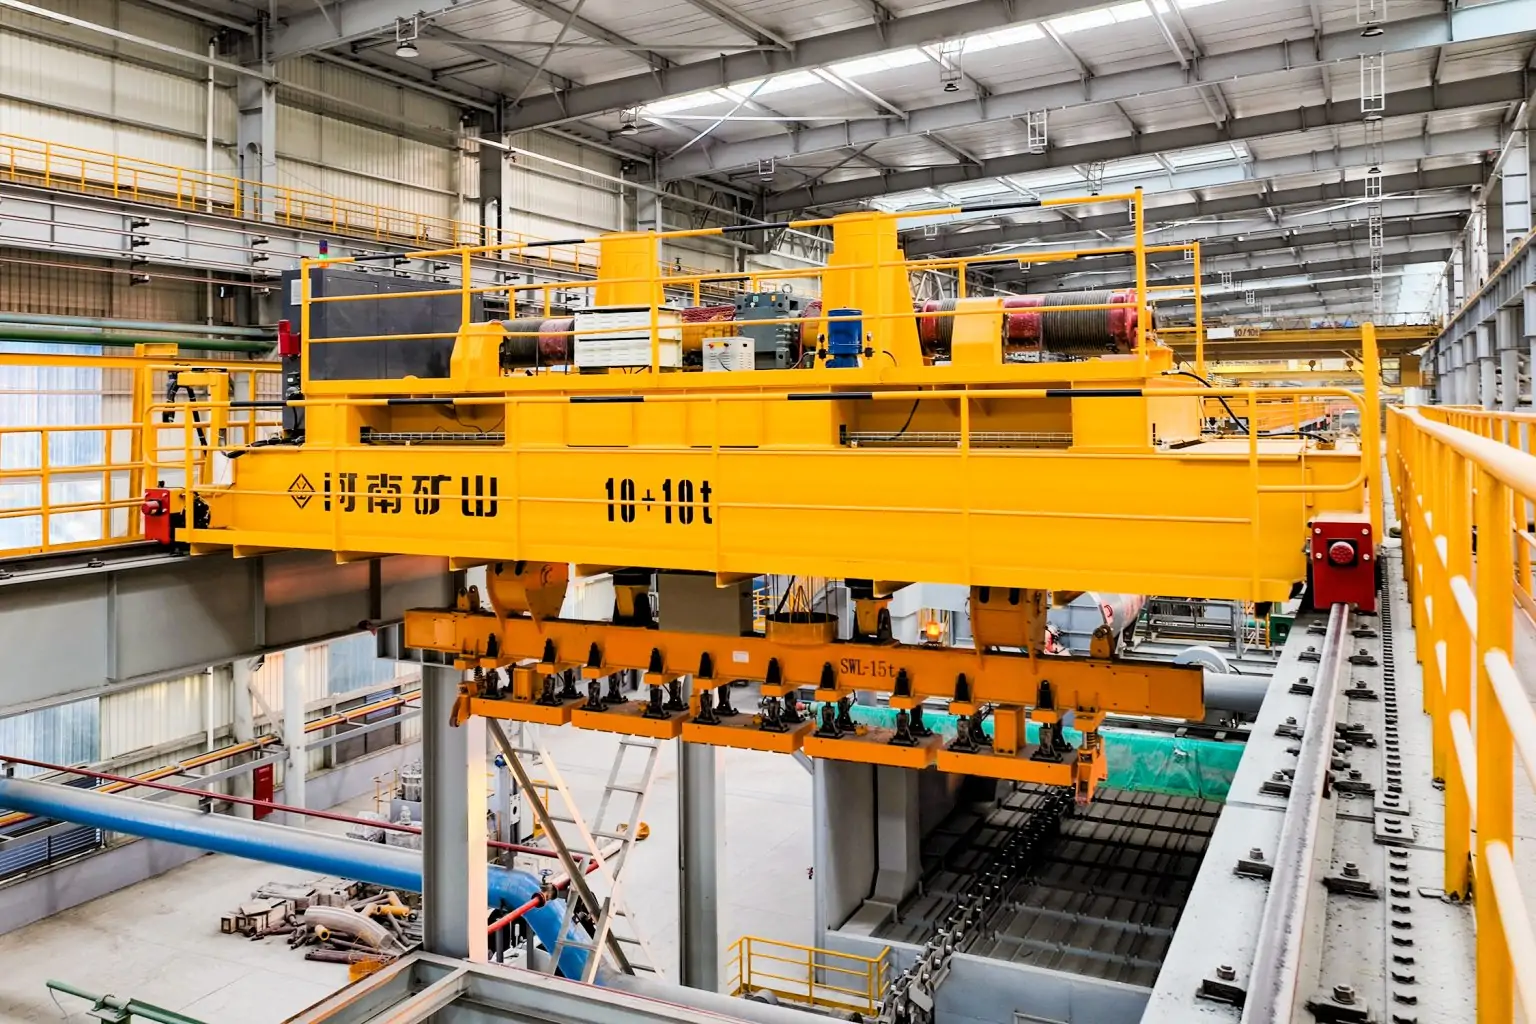
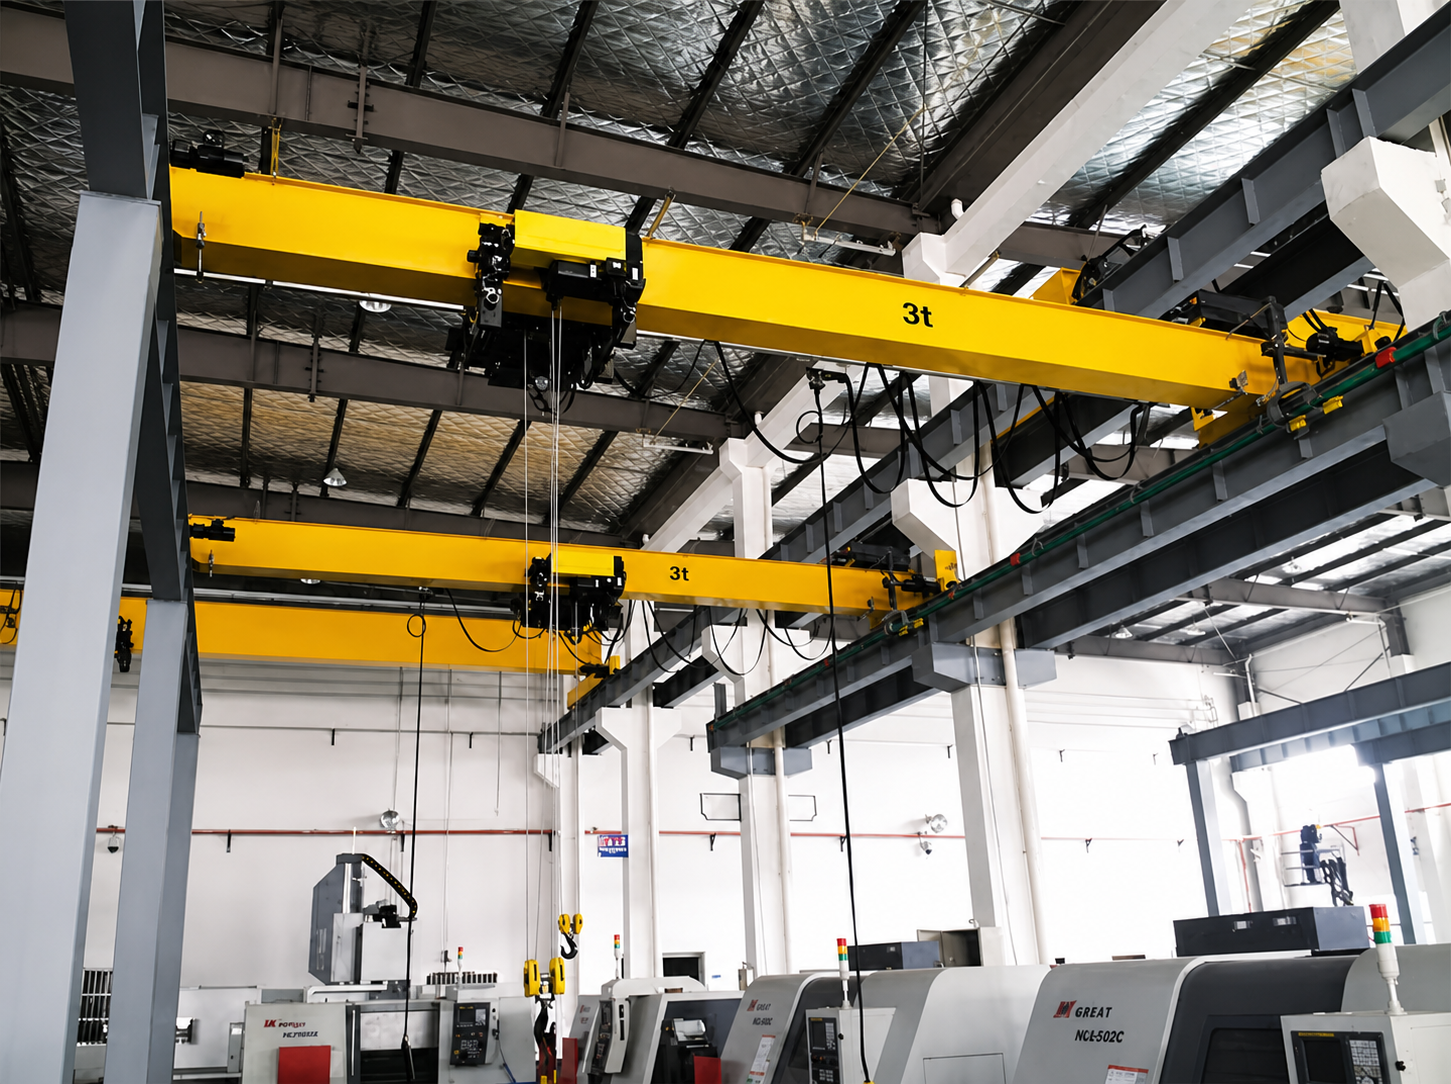
    The production efficiency of precast concrete factory mainly depends on the smoothness of component hoisting, material transfer and mold turnover.Bridge crane is the core heavy equipment of prefabricated workshop, which is suitable for demoulding, stacking and loading of various prefabricated components such as wallboard, beam column and box girder.Compared with ordinary equipment such as forklifts, special bridge cranes are more suitable for high-frequency, heavy-duty and high-precision operation scenarios in prefabricated plants, effectively solving common problems such as inefficient handling, component loss and potential safety hazards.

    At present, many prefabricated factories generally have problems such as component shaking offset, slow material flow, high labor cost, easy equipment failure and so on, which seriously affect production capacity and production safety.This guide combines the actual working conditions of the prefabricated factory to explain the application value, selection points, efficient configuration and cost reduction scheme of the overhead crane in detail, helping practitioners to select products scientifically, standardize the use of equipment, avoid procurement and operation errors, and effectively improve the production efficiency of the workshop.

    Why Precast Concrete Factories Need Bridge Cranes

    Heavy component handling

    Precast concrete members are generally heavy and bulky, and ordinary handling equipment cannot meet the heavy lifting requirements.Henan Mine Crane manufactured bridge crane for prefabricated factory supports 5 – 300 tons of load and is suitable for all kinds of components such as beam column, wall plate and box beam.The equipment adopts high-strength main beam and heavy winch structure, which is stable and not easy to deform. It supports single-point and double-machine synchronous hoisting, and can easily handle overweight, extra-long and extra-wide component operations. It is the core and efficient equipment for heavy load handling in prefabricated factories.

    Faster material flow

    Prefabricated production is an assembly line operation, and the material flow efficiency directly determines the production capacity.Bridge crane relies on the workshop top rail full coverage operation, no ground blind area, can complete the mold lifting, component displacement, demoulding transfer, finished product loading and other full process procedures.Compared with the short board with limited forklift operation range, it can quickly schedule across stations, speed up mold turnover, eliminate material accumulation and idle station problems, effectively open up production blocking points, and comprehensively improve workshop circulation efficiency.

    Improved workplace safety

    Heavy-load hoisting in prefabrication plant belongs to high-risk process, and manual auxiliary simple equipment has many hidden dangers.The special bridge crane is equipped with a complete set of safety systems such as overload limit, emergency braking, anti-swing, etc. to avoid the risks of lifting fall, overload, deviation, etc. from the source.The whole process of mechanized operation of equipment does not require manual close contact with heavy load areas, avoiding the problem of component collision with equipment and walls, greatly reducing the probability of safety accidents, and comprehensively improving the safety production level of workshops.

    Reduced labor costs

    The traditional prefabricated component hoisting needs many workers to work together, with large manual investment, low efficiency and high cost.Henan Mine Crane manufactured  Intelligent bridge crane can realize single independent operation, greatly reducing the number of post workers.Equipment operation is simple, ordinary employees can be trained simply, reducing the cost of technician recruitment and training.At the same time, equipment operation and maintenance is convenient and stable, reducing manual maintenance investment, avoiding rework losses caused by operation errors, and saving the factory a lot of labor costs in the long run.

    How to Select the Right Bridge Crane for Your Factory

    Lifting capacity

    Lifting tonnage is the core parameter of overhead crane selection, which is related to operation safety and production adaptability.The model selection shall be based on the maximum prefabricated component weight of the factory, superimposed with the weight of the lifting appliance, and reserve 10%-20% safety load margin to prevent the equipment from long-term overload operation.Small prefabricated components are suitable for medium and small tonnage models, box girders, large wall panels and other heavy-duty components, and large-tonnage double-beam cranes are required to be selected, giving consideration to equipment operation safety and procurement cost performance.

    Crane span

    Henan Mine Crane manufactured crane span is the center distance of the rails on both sides, which directly determines the coverage of equipment operation and needs to match the actual width of the prefabricated workshop.The span is too small to leave operation blind area, relying on manual auxiliary transportation.If the span is too large, it will increase the equipment cost, increase the running inertia and reduce the lifting accuracy.The normal span of prefabricated workshop is 12 – 36m, standard workshop adopts standard model, and ultra-wide and special-shaped workshop can customize non-standard span to ensure no blind area operation in the whole area.

    Hook height

    The lifting height of hook determines the maximum vertical height of lifting operation, which is suitable for core procedures such as demoulding, component stacking and high loading in prefabricated plant.The model selection shall be combined with the clearance height of the plant, mold size, component height and stacking layers, and sufficient safety margin shall be reserved to prevent the hook top rail and components from colliding with the top of the plant.Conventional workshop is suitable for lifting height of 6 – 18 meters, high workshop, multi-layer stacking operation scene, and can customize heightening models to meet the lifting requirements of the whole scene.

    Product types

    Bridge cranes are mainly divided into single beam and double beam, which can be flexibly selected according to production conditions.Single beam crane structure light, cost-effective, suitable for small and medium-sized components and medium frequency light load operation, suitable for small and medium-sized prefabricated factories.Double-beam crane has strong bearing capacity, high precision and working system up to A7-A8, which can meet the continuous production of high frequency and heavy load. It is the first choice for large component production.Special dust, corrosion conditions, but also customized explosion-proof, anti-corrosion special models.

    Factory layout

    The overall layout of workshop is the key basis for crane selection, which directly affects the installation effect and operation efficiency of equipment.Before selection, it is necessary to sort out the distribution of work stations, material circulation, finished product stacking and loading area layout. The dense work stations are suitable for high-precision double-beam cranes, and the narrow workshops are matched with customized stroke models.The large-scale partitioned workshop can be configured with multiple equipment for partitioned operation, and at the same time check the load bearing and track installation conditions of the workshop to ensure that the equipment is suitable for the site and does not occupy the ground production space.

    Bridge Crane

    Key Bridge Crane Features That Improve Production Efficiency

    Anti-sway control

    Precast concrete members are large in volume and inertia, and are easy to shake and deviate during lifting and movement, which not only reduces alignment efficiency, but also easily causes collision and damage of members, resulting in potential safety hazards.Henan Mine Crane manufactured bridge crane equipped with intelligent anti-swing control system can measure and correct the swing amplitude of the lifting object in real time, accurately suppress the vertical and horizontal two-way shaking, and make the component start and stop smoothly and accurately.Without manual auxiliary correction, it can not only improve the fine operation efficiency of demoulding and stacking, but also effectively reduce the damage loss of components and ensure the construction safety.

    Variable speed drive

    The traditional fixed-speed crane has large start-stop impact and fixed speed, which is difficult to meet the fine hoisting requirements of prefabricated components, and is prone to component deviation, mold collision and other problems.Variable frequency speed drive system supports stepless speed change free switching, long-distance transfer can run at high speed, save working hours, demoulding, alignment, loading process can be adjusted at low speed, smooth operation without impact.At the same time, it can reduce equipment start-up energy consumption and mechanical wear, prolong equipment service life, and give consideration to operation accuracy, efficiency and equipment operation stability.

    Dual hoist design

    Box girder, long beam column and other ultra-long prefabricated components, single-point lifting is easy to bear uneven force, resulting in bending, cracking, tilting and other scrap problems.Double hoist synchronous bridge crane equipped with double sets of linkage lifting mechanism, can achieve two-point synchronous lifting, translation, uniform distribution of component stress, from the root to avoid deformation damage.The equipment supports two modes of synchronous heavy load hoisting and independent light load operation. One machine has multiple uses and wide adaptability, effectively solving the hoisting problem of irregular strip members and significantly improving the qualified rate of finished products.

    Remote operation

    Prefabricated special bridge crane equipped with remote control, cab dual operation mode, wireless remote control more practical.Operators can work in the best vision area, avoid the blind area of cab vision, accurately adjust the lifting track, and eliminate alignment deviation and component collision problems.A single person can complete a full set of lifting procedures, flexible operation, rapid response, effectively shorten the operation time.At the same time, it can keep operators away from dust and heavy-duty high-risk areas, perfectly adapt to the harsh working environment of prefabricated workshops, and greatly improve operation safety.

    Heavy-duty performance

    Prefabricated factories are mostly 24-hour high-frequency and heavy-duty continuous operations, which require extremely high stability and durability of cranes.Special heavy-duty overhead crane adopts flaw detection heavy girder, anti-deformation, impact resistance, with heavy-duty special core accessories, suitable for A7-A8 high-grade working system.The whole machine adopts dustproof, waterproof and anti-corrosion protection design, which can resist dust, humidity, temperature difference and other bad working conditions in the workshop. It has low failure rate, stable operation, all-weather continuous operation, and effectively guarantees uninterrupted and efficient operation of the prefabricated production line.

    Common Lifting Challenges and Practical Crane Solutions

    Preventing concrete damage

    The quality of incipient wet concrete component is fragile, and the traditional lifting is easy to crack, drop angle, deformation and other problems, resulting in product scrap and economic loss.Prefabricated special bridge crane equipped with anti-swing and frequency conversion stable start-stop system, can eliminate lifting shock and shaking.With flexible lifting tools and balanced lifting point design, uniform distribution of component stress, with accurate fast and slow control, to achieve stable alignment landing, effectively protect the integrity of components, greatly reduce the damage rate of prefabricated products.

    Lifting long components

    It is difficult to lift super-long prefabricated beams, wall panels, pipe piles and other components. Single-point lifting is easy to cause sag, bending, cracking and deviation problems.Double hoist synchronous bridge crane can realize symmetrical lifting of double lifting points, evenly distribute force, offset bending stress, and keep horizontal and stable movement of components throughout the process.For ultra-long and heavy components, it can also support double-machine coordinated lifting, perfectly solve the handling problem of strip shaped components, and adapt to various large-scale prefabricated components production operations.

    Precise load positioning

    Demoulding, alignment, stacking, loading and other processes of prefabricated components require extremely high positioning accuracy, and slight deviation will affect the quality of finished products and production schedule.Ordinary cranes are difficult to fine-tune, positioning errors are large, and it is difficult to meet the needs of fine production.Henan Mine Crane manufactured special bridge crane is equipped with frequency conversion fine-tuning and intelligent positioning system to realize millimeter precise alignment, start and stop without inertia offset, and cooperate with remote control precision control to effectively reduce rework adjustment and greatly improve lifting accuracy and overall production efficiency.

    Harsh environment operation

    Prefabricated workshop perennial high dust, high humidity, poor working conditions, common crane easy to rust, dust accumulation, circuit failure, frequent failure to stop delay production.Special heavy duty bridge crane through dust, waterproof, anti-corrosion strengthening treatment, electrical protection level up to IP 55 or above.Metal structure rust and wear resistance, moving parts equipped with dust protection structure, can adapt to all-weather continuous operation, low failure rate, low operation and maintenance pressure, effectively ensure long-term stable operation of the production line.

    How bridge cranes increase productivity and reduce costs

    Faster production cycles

    With its efficient global handling capability, Henan Mine Crane manufactured bridge crane effectively compresses the overall production cycle of prefabricated components and breaks through the pain points of traditional handling procedures.The equipment is suitable for the whole process lifting operation, which can quickly complete the mold turnover, component transfer and finished product delivery, and quickly empty the station, so that the production line can seamlessly connect the next batch of production.The stable and high-frequency operation mode greatly improved the process circulation efficiency, effectively accelerated the workshop production cycle, and significantly improved the overall turnover rhythm.

    Higher daily output

    Smooth material flow and stable operation of equipment can directly increase the daily production capacity of the prefabrication factory.The bridge crane has no blind area and full coverage operation, so that each station in the workshop can operate efficiently, and the waste of production capacity such as material accumulation, idle station and equipment shutdown can be eliminated.At the same time, the accurate and stable lifting method reduces component scrapping and rework adjustment, improves effective production time, continuously and stably improves the daily output of finished products, helps the factory to expand production scale and improves order delivery efficiency.

    Lower operating costs

    Bridge cranes for prefabricated plants reduce long-term plant operating costs from multiple dimensions.Intelligent operation greatly reduces manual input, frequency conversion energy-saving technology effectively reduces equipment energy consumption, solid fuselage structure reduces failure and maintenance expenses.Accurate lifting can effectively avoid component damage and scrap, reduce raw material loss and rework costs.Although the initial investment of equipment is higher, with the advantages of low energy consumption, low operation and maintenance and low loss, it can quickly recover costs and continuously improve the profitability of the factory.

    Better space utilization

    Traditional floor handling equipment occupies a large number of workshop passages and working space, resulting in low utilization of prefabricated workshop space.The overhead crane adopts the top rail suspension design, which does not occupy the floor space at all, and can maximize the free workshop area for mold placement, component maintenance and finished product stacking.The operation track covered by the equipment can flexibly handle materials in narrow corner areas without reserving a large number of passages, helping small and medium-sized limited plants to achieve efficient expansion and production increase.

    Reduced product loss

    Precast concrete component raw material cost is high, lifting bump, deformation and cracking will cause serious economic losses.The special bridge crane is equipped with anti-swing, stable start and stop, accurate alignment functions, uniform lifting force, reducing the probability of component damage, collision and deformation from the source, and greatly reducing the scrap rate of products.At the same time, it reduces the damage of molds and equipment caused by lifting errors, effectively improves the yield of finished products, reduces ineffective losses, and maximizes production benefits.

    Henan Mine Crane Factory Custom

    Precast concrete factory has its own production demands, including component sizes, maximum lifting weight, workshop layout as well as the working frequency. Henan Mine Crane Factory offers tailor-made bridge crane solutions to adapt to production processes for precast concrete factories, aiming at a safe materials lifting, smooth material flow, improved positioning accuracy and long-term safe operation. With state-of-the-art manufacturing technology, rigorously CE certified quality assurance and vast experience in heavy crane engineering, each solution is ready to work in tough industrial conditions.


    Regardless you want to establish a new precast concrete plant or upgrade a existing production line, selecting the right bridge crane supplier could be a life-time success with high productivity and low operating cost. Henan Mine Crane Factory provides professional engineering consultancy, customized crane design and engineering, on-site installation supervision and after-sales rapid service for the customers to achieve a kind of production efficiency increase by saving maintenance cost.

    Henan Mine CraneDiscuss your requirements ↗
  • Brazil Mining Gantry Crane Supplier: Heavy-Duty Solutions for Maintenance Yards and Outdoor Handling

    Brazil Mining Gantry Crane Supplier: Heavy-Duty Solutions for Maintenance Yards and Outdoor Handling

    Brazil Mining Gantry Crane Supplier: Heavy-Duty Solutions for Maintenance Yards and Outdoor Handling

    Brazil is the world’s core mineral resource producer, iron ore, manganese ore, bauxite and other minerals mining and transportation industry is huge. From the mining area of Minas Gerais plateau to the mining belt around the Amazon in Pará state, and then to the ore transshipment yards along the coast, a large number of outdoor operation scenarios have stringent requirements for lifting equipment.

    Brazilian mines are mostly open-air operations, both tropical heat, rainy season storm wash, dusty working conditions all year round, ordinary industrial lifting equipment is difficult to operate stably for a long period of time. Mining gantry cranes, as the core equipment for mine maintenance, material transfer, yard loading and unloading, cover almost all large and medium-sized Brazilian mining projects and supporting outdoor yards.

    Brazil local mining procurement team in screening Brazil mining and yard gantry crane supplier, will not only compare the initial purchase price. With the complexity of outdoor working conditions and the high cost of downtime, the durability of the equipment, climate suitability, long-term maintenance costs and stable spare parts supply are the core basis of the purchasing decision. This article combines the characteristics of Brazil’s local mining sites, talk about mining and outdoor yards how to select the appropriate gantry crane manufacturers.

    Why the Brazilian mining industry and yard operations need reliable suppliers of gantry cranes

    Mining and yard operation conditions are extremely harsh

    Brazil’s major mining areas generally adopt all-weather continuous operation mode, daily need to frequently lift heavy mining parts, large molds, bulk ore supporting materials, lifting loads, the frequency of operations is intensive. Most of the operation areas are completely open-air, without any plant shelter protection.

    Geographical and climatic differences further exacerbate the wear and tear of equipment, high temperature and humidity in the rainforest region of northern Brazil, rainy all year round, the central plateau mining area, the dry and rainy seasons, the rainy season, more than short-term rainstorms, the south and the coastal yards are also corrosive salt spray problems. Long-term heavy loads superimposed on bad weather erosion, the equipment structure and core components are a great test.

    Crane stability directly determines the efficiency of site operations

    Mining material transfer, equipment dismantling and maintenance, yard cargo loading and unloading, all rely on gantry cranes articulated propulsion. Once a sudden equipment failure and shutdown, the entire operation chain will be directly interrupted, material accumulation, equipment stagnation, schedule delays and other problems will occur simultaneously.

    For large-scale mines and foreign trade ore yards, each unplanned downtime will produce high direct and indirect losses, stable equipment operation is the basis for guaranteeing production capacity.

    Outdoor scenarios require higher structural design of equipment

    Brazil’s outdoor mining areas are constantly exposed to strong winds, sunshine, heavy rain and dust, and there is also the risk of salt spray corrosion in the coastal transshipment yards. Ordinary standard gantry cranes are only suitable for indoor mild working conditions, steel structure paint, electrical sealing, core protection can not be adapted to the complex outdoor environment.

    Without special optimization of the equipment put into use in Brazilian mines, the paint will peel off in a short time, steel structure corrosion, electrical moisture short-circuit, wear and tear of walking parts jamming and other problems, the failure rate remains high. Only the Brazilian outdoor gantry crane manufacturer ‘s products that are designed for outdoor enhancement can be adapted to local long-term operational needs.

    Purchasers pay more attention to the value of the whole life cycle of the equipment

    At this stage, Brazil’s large mining enterprises, foreign trade yards, ports supporting mining projects, procurement logic has been very mature. Screening Brazilian yard gantry crane suppliers, will focus on considering the durability of the equipment structure, adaptability to working conditions, annual maintenance costs and long-term after-sales capacity, and prioritize the selection of heavy-duty adapted equipment with a higher overall cost-effective.

    Types of Gantry Cranes Commonly Used in Brazilian Mining and Yard Projects

    Single Girder Gantry Crane

    Single girder gantry cranes are lightweight, easy to install, and have outstanding cost performance. They are mainly suitable for light and medium load operation scenarios such as auxiliary operation areas in Brazilian mining areas, small material yards, and daily maintenance of workshops. Mostly used for small parts transfer, tool stacking, light equipment disassembly and assembly and other routine work.

    Equipment for the site foundation requirements are low, suitable for most of the small and medium-sized mining supporting sites, is the Brazilian small and medium-sized mining projects use the highest rate of basic models.

    Single-girder gantry crane 10 ton

    Single-girder gantry crane manufactured by Henan Mine Crane

    Double Girder Gantry Crane

    Brazilian double girder gantry cranes are the core equipment in large mining areas, heavy-duty yards, and ore transfer sites in ports. The double girder steel structure is more rigid, with sufficient load capacity, better resistance to deformation and wind, and can be adapted to large tonnage and heavy load, large span coverage, and high-frequency continuous outdoor operation.

    Heavy-duty double girder gantry cranes are basically used for heavy-duty mining machine lifting, large component transfer, and bulk ore material loading and unloading in large iron ore and manganese ore mines in Brazil, and they are also the mainstream selection of heavy-duty gantry cranes in the mining industry.

    MG double girder gantry crane design

    Henan Mine Crane’s MG double girder gantry crane

    Semi-portal Crane

    Semi-gantry cranes run unilaterally on existing workshop walls and plant columns, and lay ground tracks unilaterally, without the need to remodel the site infrastructure in the whole area. It is suitable for the operation area of the existing plant in the mining area, and the indoor and outdoor articulation of the maintenance workstations.

    It can effectively utilize the existing building structure, save the cost of track laying and site reconstruction, and is suitable for supporting workshops in mining areas with limited space.

    MGB semi-gantry crane custom

    The MGB semi-gantry crane manufactured by Henan Mine Crane

    Tire Gantry Crane

    In Brazil, some temporary mining operation areas, staged material dumps and remote mining areas do not have fixed track laying conditions. Tire gantry cranes do not need rail support, and can be freely moved to change positions, so they are highly adaptable to the site.

    This type of equipment is highly flexible, can follow the operating area to adjust the position, perfectly adapted to the stage of the project, multi-site decentralized operations, remote mining sites with weak infrastructure.


    Customized Mining Gantry Cranes

    Many large-scale mining projects in Brazil use customized gantry cranes for special scenarios such as ore bulk material grabbing, precise dismantling of heavy equipment, and special loading and unloading of bulk materials. It can be equipped with hydraulic grab, special spreader, shaped spreader and other exclusive accessories.

    At the same time, according to the site wind, humidity, corrosion, customized to strengthen the anti-corrosion, wind, dust-proof configuration, fully adapted to the differentiated mining conditions in Brazil.

    Core application scenarios of gantry cranes in Brazil’s mining industry and stockyards

    Mining equipment maintenance yard

    Core equipment such as crushers, conveyor pumps, large motors, gearboxes, conveyor units, etc. in major open-pit mines in Brazil need to be regularly dismantled for maintenance and replacement of parts. Gantry Cranes are the core equipment for lifting, dismantling and resetting such heavy equipment.

    The stability of equipment operation directly affects the maintenance efficiency, which can effectively shorten the length of production line downtime for maintenance and protect the continuous production rhythm of the mine.

    Outdoor Material Storage Yard

    A large number of steel structure profiles, pipe fittings, spare machinery and ore supporting materials in the mining area will be centrally stacked in the outdoor yard. Gantry Cranes have a wide coverage and strong carrying capacity, and can complete a wide range of material stacking, transfer, and regularization work.

    Compared with small handling equipment, gantry cranes are able to cover large-span yards and meet the demand for centralized operation of bulk materials.

    Bulk material and industrial logistics area

    Gantry cranes undertake the core transshipment work in Brazil’s ore outbound transportation, material transshipment, and project freight loading and unloading scenarios. It can assist the loading, unloading and inter-area transfer of heavy mining materials, industrial consumables and project equipment.

    Adapt to the high-frequency operation demand of the logistics chain in the mining area, and open up the material flow link from mine production to external transportation.

    Workshop Maintenance Supporting Operations

    Supporting maintenance workshops and equipment repair work areas in the mining area need gantry cranes to assist workpiece handling, equipment assembly and replacement of faulty parts. Support the workshop normalized equipment repair work, to ensure the normal operation of various types of machinery in the mine.

    Port-linked mining yards

    Several ore export ports along the Brazilian coast are equipped with a large number of mining transit yards. Such sites need gantry cranes to assist the export of ore materials stacking, container parts loading and unloading, outbound equipment maintenance operations.

    At the same time to adapt to the coastal high salt spray corrosive conditions, the need for equipment with stronger corrosion and weather resistance.

    Core advantages of gantry cranes adapted to mining and yard operation

    Suitable for all-open-air outdoor operating environment

    Overhead Cranes must be installed and used in closed plants, while Gantry Cranes do not need to be supported by a complete building structure, and can be directly landed in open mines, open yards, and field operation sites.

    It perfectly matches the Brazilian mining industry’s production mode, which is mainly based on open-air operation, and is not restricted by the infrastructure of the plant, so it is highly adaptable to the ground.

    Can cover a large operating area

    The span and running length of the gantry Crane can be customized to meet the operational needs of Brazil’s large open dumps, long strip mining areas and decentralized maintenance areas.

    The equipment can cover a wide range of blind areas, so that the material transfer, equipment lifting without dead ends, to enhance the overall consistency of operations.

    Suitable for all kinds of heavy-duty lifting needs

    Especially heavy-duty double girder gantry cranes, with a wide tonnage coverage and sufficient structural capacity, can easily cope with heavy equipment and large-volume material lifting operations in mining areas.

    It can withstand high frequency and large load cyclic operation for a long time, which is suitable for high-intensity production conditions in the mining industry.

    Suitable for remote and undeveloped infrastructure project sites

    In Brazil, some remote inland mining areas and new operating sites have weak infrastructure, and there is no perfect plant and lifting infrastructure. Gantry Cranes have low requirements for site infrastructure, simple installation conditions and fast landing speed.

    It can quickly make up for the lifting operation short board in remote mining areas and help the project go into production quickly.

    Brazilian mining industry procurement focus on the core technical parameters to consider

    Rated lifting capacity

    Tonnage selection needs to refer to the site’s maximum lifting load, including heavy mining machines, mold parts, the maximum weight of bulk materials, while leaving enough safety margin, to prevent full load, overload operation.

    Brazil’s small and medium-sized yards routinely use 10-30 tons of models, large mining heavy-duty operations generally use 50 tons and above heavy-duty gantry cranes.

    Equipment span

    The span size needs to accurately match the width of the yard, the spacing between maintenance stations and the actual size of the material working area. Insufficient span will create a blind spot in the operation, while too large a span will result in a waste of equipment resources.

    Professional manufacturers will combine the drawings of the Brazilian mining site and the topography of the site to customize the appropriate span size.

    Lifting height

    The lifting height needs to meet the requirements of equipment maintenance and hoisting, material stacking, and site safety clearance, and at the same time, take into account the operating safety distance in Brazil’s rainy season, heavy rain and windy weather.

    Adequate vertical working space is reserved to avoid shaking and collision of materials and equipments and to ensure the safety of operation.

    Running Length

    The running length of the railroad track directly determines the horizontal working coverage of the equipment. It needs to match the overall layout of the production line, yard partition, and maintenance area in the mining area to ensure the full coverage of the whole process operation.

    Working Level

    The Brazilian mining industry and outdoor yard are high-frequency cyclic operations, and the use of light civil grade equipment is strictly prohibited. Medium grade equipment can be used in regular auxiliary work areas, while medium and heavy grade equipment must be used in core production, heavy load transfer and high frequency maintenance areas.

    Low-grade equipment adapted to mining conditions for a long time will quickly develop structural fatigue and component damage, posing great safety risks.

    Maneuvering mode

    Light material transfer, routine maintenance work, can choose the handle wired control, operation is simple and easy to get started. For outdoor large-scale and high-frequency operation, wireless remote control is preferred for flexible operation and higher operational safety.

    Large tonnage and heavy load, high-precision alignment operation scenarios, can be matched with the cab control, wider field of vision, more stable control accuracy.

    Power supply conditions

    The power supply conditions in Brazil’s remote mining areas and newly-built yards are unstable, and some sites do not have standardized industrial power supply. The electrical system of the equipment needs to be adapted to the local power supply parameters, and the manufacturer can customize the adapted power supply solution to match the actual power conditions of the site.

    Brazilian mining gantry cranes in the core of the harsh working conditions of the key points

    All-weather outdoor climate erosion

    Brazilian mining areas are hot and sunny all year round, with frequent concentrated rainstorms in the rainy season and high air humidity. The electrical system, paint, and metal structure of ordinary equipment are susceptible to moisture, corrosion, and aging when exposed to such environments for a long period of time.

    Equipment adapted to local working conditions must be well designed for waterproof, rainproof, sunscreen and sealing protection to enhance outdoor weather resistance.

    Dusty and dirty working environment

    Mining, material stockpiling, loading and unloading operations will continue to produce a large amount of ore dust, which is very easy to adhere to the motor, brake, wheels, electrical switches and other core components, resulting in component blockage, increased wear and circuit failure.

    Mining special-purpose gantry cranes need to optimize the dust-proof structure, and key operating components are equipped with sealing protection devices to reduce the wear and tear of dust on the equipment.

    Coastal and highly corrosive site risk

    Brazilian coastal ore yards, ports supporting mining areas, the air contains salt spray components, extremely corrosive to the steel structure. Ordinary paint spraying process will cause skinning, rusting and peeling problems in a short period of time.

    For coastal corrosive conditions, it is necessary to upgrade the heavy-duty anticorrosive coating process, multi-layer protective paint superimposed to enhance the equipment’s salt spray and corrosion resistance, suitable for long-term outdoor coastal operations.

    Long-term continuous operation cycle

    Brazil’s large-scale mining areas and foreign trade yards, commonly used in two shifts, three shifts non-stop mode of operation, gantry cranes daily operating hours are extremely long, the core components continue to operate at high frequency.

    This requires that the core components of the equipment must be selected for heavy-duty configuration to meet the needs of uninterrupted operation for a long period of time, to avoid rapid aging and failure of the components.

    Large irregular yard terrain

    Many outdoor mining yards in Brazil have a wide area and uneven terrain, so there are limited conditions for track laying. Manufacturers are required to optimize the track layout and wheel pressure distribution scheme according to the site topography to avoid problems such as equipment deflection, shaking and uneven force.

    Core criteria for quality Brazilian mining gantry crane suppliers

    Complete independent production strength

    A reliable Brazilian industrial gantry crane supplier must have independent steel processing, complete machine assembly, load testing, anti-corrosion treatment, electrical commissioning of the whole process capacity, and never a simple equipment assembly trader.

    Independent production in order to control the welding process, structural thickness, component quality, corrosion standards from the source, to ensure that the equipment is suitable for heavy-duty outdoor working conditions in Brazil. Henan Mine Crane has an intelligent production base for heavy-duty lifting equipment, with complete export qualifications, and can customize special equipment for Brazilian mines in bulk.

    Rich experience in outdoor mining projects

    Ordinary industrial Crane manufacturers are only familiar with the indoor mild working conditions, do not understand the Brazilian mining areas of high temperature, heavy rain, dust, corrosion of the special operating environment, the design of the equipment is very easy to appear incompatible with the problem.

    Professional export manufacturers are deeply rooted in the Brazilian mining market, familiar with the local mining climate characteristics, site conditions, operating habits and import acceptance standards, can optimize the equipment program.

    Professional engineering customization and adaptability

    Each Brazilian mining site has different site dimensions, operating frequency, material types and environmental conditions, so standardized general equipment cannot be fully adapted. High-quality manufacturers can optimize equipment parameters, protection configurations, and functional modules according to customer drawings, site photos, and operational requirements.

    Stringent full-dimensional quality control

    The quality control of mining gantry cranes runs through the entire production process, including weld flaw detection, structural dimension calibration, machine load testing, electrical safety testing, anticorrosion paint testing and other core aspects.

    All equipment must be completed before leaving the factory, no-load, full-load, overload test, to check all kinds of hidden dangers, to ensure that the equipment can be put into heavy-duty operation directly after landing in the mine.

    Perfect after-sales and spare parts supply system

    Brazilian mining areas have a large geographical span and some sites are remote, so if the equipment fails to maintain and replenish spare parts in time, it will cause long-term downtime and wear and tear. High-quality foreign trade manufacturers can provide English technical docking, remote troubleshooting, installation and commissioning guidance services.

    At the same time, reserve common wearing parts, shorten the cross-border maintenance cycle, to ensure the continuous and stable operation of equipment.

    Brazilian project gantry crane supplier assessment methods

    Verification of similar overseas landing project cases

    Before cooperation, focus on verifying whether the manufacturer has real landing experience in Brazilian mines, outdoor yards, port mining support, heavy maintenance projects. Manufacturers with local mature projects, program suitability and equipment quality is more guaranteed.

    Verification of a full set of standardized technical data

    Regular manufacturers can provide a complete set of equipment assembly drawings, technical parameter tables, electrical schematic diagrams, wheel pressure load data, parts lists, factory quality inspection reports. For export projects to Brazil, we can provide a full set of English compliance data to facilitate customs clearance, factory acceptance and equipment archiving.

    Confirmation of core component brands and configurations

    Core components such as motor, reducer, brake, electrical components, wire rope, traveling wheels, etc. directly determine the stability and service life of the equipment. When purchasing, it is necessary to clarify the brand, protection level and specification parameters of each component to eliminate low-component replacement.

    Verification of factory testing and quality inspection process

    Require manufacturers to provide complete factory inspection records, including appearance testing, size verification, no-load test run, full-load load test, electrical safety testing and other complete sets of quality inspection information to ensure that the equipment has no hidden quality problems.

    Define the scope of delivery and installation services

    Confirm the scope of cooperation in advance, and make clear whether it includes equipment delivery, track matching, installation guidance, on-site commissioning, personnel training and other services. Overseas projects have a high threshold for installation, and professional technical guidance can avoid problems such as irregular installation and inadequate commissioning.

    Brazilian Mining Crane Project Procurement Common Concerns

    Whether the equipment is suitable for long-term outdoor heavy-duty operations

    Many low-priced equipment is only labeled with nominal tonnage, thin steel structure, insufficient spare parts, no outdoor protection design, and can only be adapted to occasional light work. Long-term operation in Brazilian mining areas under heavy load, sunshine and rainstorms will easily lead to structural deformation and component damage.

    Whether it can safely complete the maintenance of mining equipment

    Mining equipment is extremely heavy and structurally precise, and unstable lifting start and stop, shaking and shifting will easily cause damage to the equipment. Mining special gantry cranes will optimize the braking system, smooth start-stop design, suitable for heavy equipment lifting maintenance operations.

    Whether the equipment structure can withstand bad weather and dust environment

    Ordinary equipment without special protection, in Brazil, high temperature, rain, dust, corrosion conditions, short-term paint peeling, steel corrosion, electrical moisture failure and other problems. Professional mining equipment will do dustproof, waterproof, anti-corrosion triple protection upgrade.

    Can the spare parts be replenished quickly?

    The logistics turnover in remote mining areas in Brazil is slow, and the procurement cycle of niche accessories is long. When purchasing, you need to confirm the manufacturer’s cross-border parts inventory, replenishment cycle and logistics capabilities to ensure that the equipment can be quickly repaired after failure.

    Whether the quotation includes a full set of ancillary services and accessories

    Some of the low-priced offers only include the host equipment, excluding tracks, electrical packages, anticorrosion treatment, commissioning services, spare parts, which will generate a lot of invisible incremental costs later on, raising the overall landed cost.

    Customization of special spreader and special functions

    Special scenarios such as ore bulk material grabbing, heavy component lifting, precise alignment, etc. require exclusive spreaders and functional configurations. High-quality manufacturers can customize grabs, spreader, anti-shaking, frequency speed control and other personalized configurations.

    How to horizontally compare the Brazilian gantry crane manufacturers offer

    Eliminate a single price to determine the advantages and disadvantages of equipment

    Mining outdoor lifting equipment belongs to the heavy-duty industrial equipment, price and quality are highly compatible. Most of the low-priced program corresponds to lightweight structure, low-end components, simplified protection configuration, short-term savings, long-term failures are frequent, downtime loss is huge.

    Brazilian mining projects place more importance on the long-term stable operation of the equipment rather than the initial purchase price difference.

    Line-by-line comparison of the full set of technical configuration details

    When comparing horizontally, it is necessary to unify and check the details of steel structure material and thickness, lifting mechanism configuration, braking system, electrical protection level, control mode, outdoor anticorrosive coating, safety devices, spare parts, installation and commissioning services, and so on.

    Only the configuration dimension is unified, in order to realize a fair comparison, to avoid being misled by the low-cost program.

    Focus on checking the work level and working condition suitability

    It must be confirmed that the equipment is designed according to the Brazilian mining industry’s outdoor heavy-duty standard, and is suitable for high-frequency continuous working conditions, rather than the general indoor lightweight standard. Mismatch in working conditions is the core reason for frequent failures and shortened service life of the equipment.

    Focus on warranty terms and long-term after-sales system

    Warranty period, warranty coverage, cross-border after-sales response time, spare parts supply capacity, is the core of the long-term stable operation of the equipment to ensure. A perfect service system can minimize the risk of downtime in the mining area.

    Project information to be provided by Brazilian mining docking manufacturers

    Basic technical parameters

    Sort out in advance the rated lifting capacity, operating span, effective lifting height, total running length of the truck, on-site power supply parameters, and preset working level required by the equipment, so as to provide an accurate basis for the manufacturers to customize the program.

    Application details of working conditions

    Clearly define the daily lifting objects, including heavy mining machines, mold parts, ore materials, engineering equipment and so on. At the same time mark the daily operation frequency, whether 24-hour continuous operation, whether there is a need for precise lifting.

    Site information

    Provide the overall layout of the yard, track foundation parameters, site flatness description, site pictures, so as to facilitate manufacturers to optimize the equipment structure and track installation scheme to fit the actual conditions of the site.

    Personalized customization requirements

    Define in advance whether there is a need for wireless remote control, cab control, frequency control, anti-shaking system, heavy anti-corrosion coating, special grapple spreader and other customized needs, so that the program and quotation in one step.

    Case study: how to choose the right supplier of gantry cranes for Brazilian mines

    A large mining yard in Minas Gerais, Brazil, is mainly responsible for the maintenance of heavy equipment in the mining area, spare parts transfer, loading and unloading of ore supporting materials, the site is always open to the sun, frequent rainstorms in the rainy season, dust, the need to purchase a heavy-duty double girder gantry cranes to adapt to the high-frequency operation.

    A number of suppliers to participate in the bidding offer, one of the local manufacturers offer lower, but the program parameters are vague, not clearly marked equipment working level, outdoor corrosion only basic painting, no targeted dust, water, windproof design, can not provide complete English technical information and remote after-sales support, and there is no similar large-scale Brazilian mines on the ground case.

    Henan Mine Crane provides a program that is fully adapted to the working conditions of Brazilian local mines, and selects heavy-duty working level, which is suitable for 24-hour high-frequency continuous operation. The equipment adopts thickened main beam steel structure, with multi-layer heavy anti-corrosion coating, full-sealed electrical protection, professional windproof and dustproof structure, which can effectively deal with high temperature, heavy rain, dust, corrosion and other harsh environments.

    The equipment is equipped with variable frequency smooth start-stop and wireless remote control system, stable lifting and accurate positioning, which can meet the dual needs of equipment maintenance and material transfer. At the same time, we provide a full set of English drawings, quality inspection reports, operation and maintenance manuals, remote installation and commissioning and personnel training.

    The mine finally gave up the low price and low allocation program and chose in-depth cooperation. After the equipment was put into operation, it has been running stably without any major faults throughout the year, with excellent performance in outdoor weather resistance and heavy-duty stability, which significantly reduces the maintenance cost and downtime loss, and provides strong support for the mine’s sustained and stable production.

    Common Procurement Misconceptions of Brazilian Purchasers

    The most common procurement problem in Brazilian mines is to take low price as the core purchasing criterion and ignore the suitability of the equipment for the working conditions. Low-matched lightweight equipment cannot withstand the high-frequency and heavy-duty operations in the mining industry, and the later operation and maintenance costs far exceed the purchase price difference.

    Neglecting the complex outdoor working conditions in Brazil, choosing common indoor standard equipment, lacking anti-corrosion, waterproof, dustproof, windproof special configuration, equipment aging speed, service life is greatly shortened.

    Without carefully checking the working level of the equipment, the company mistakenly used light equipment to replace the heavy-duty model of the mining industry, and the long-term overloaded operation is a potential safety hazard.

    Neglecting installation conditions such as track foundation, site flatness and terrain drop, resulting in the equipment running out of alignment, shaking and unable to operate at full load after installation.

    Failure to confirm the supply of spare parts and cross-border after-sales system in advance, no one to dock and no spare parts to replace the equipment after failure, resulting in long-term shutdown and production stoppage.

    Incomplete site data and working condition requirements provided at the quotation stage, leading to inconsistencies between the manufacturer’s program design and the site, repeated rectification at a later stage, and increased project costs and duration.

    Overseas manufacturers seize the core advantages of the Brazilian gantry crane market

    Scale overseas manufacturers rely on the mature production supply chain and scale production capacity, under the premise of guaranteeing the quality of heavy-duty equipment, with a stable price advantage, cost-effective than the local small workshop products.

    Perfect foreign trade export process, can provide a full set of customs clearance information, English technical documents, compliance test reports, to adapt to the Brazilian import acceptance standards. Long-term experience in overseas projects, can accurately solve all kinds of equipment in the Brazilian mining area to adapt to the problem, supporting the perfect cross-border technical guidance and delivery services.

    Brazilian Mining Gantry Crane FAQs

    What is the most suitable type of gantry cranes for mining and yard projects?

    Single girder gantry cranes are suitable for light load transshipment and small maintenance work in conventional stockyards. Double girder gantry cranes are preferred for heavy equipment lifting, large-span yards, high-frequency heavy-duty operations, and coastal corrosion sites. Temporary work without track conditions, can choose tire-type gantry cranes.

    Are double girder gantry cranes more suitable for outdoor heavy-duty operations in Brazil?

    Yes, double girder gantry cranes are more suitable for outdoor heavy-duty work in Brazil. Double girder gantry cranes have strong structural rigidity, good wind and corrosion resistance, sufficient load capacity, and more stable operation, which can be adapted to the heavy-duty, high-frequency and harsh working conditions in Brazil’s open-pit mining areas for a long time, and are the mainstream choice for large-scale mining projects.

    What working level is required for Brazilian mining yard equipment?

    Ordinary auxiliary yards can be selected for medium-duty conditions, while core production yards, equipment maintenance areas and high-frequency transfer sites must be selected for medium-heavy or heavy-duty conditions to match the intensity of daily continuous operation.

    Can a single manufacturer cover the needs of all scenarios in the yard and maintenance?

    Professional large-scale manufacturers can provide one-stop support for a full range of models, covering single girder, double girder, semi-portal, tire-type equipment, suitable for mining maintenance, yard transshipment, port supporting the full range of scenarios, and a unified after-sales system to reduce the cost of operation and maintenance of the docking.

    What core technical documents do I need to ask for before placing an order?

    Equipment assembly drawings, data sheets of technical parameters, electrical schematic diagrams, wheel pressure load data, core component brand list, a full set of factory quality inspection reports, operation and maintenance manuals, export projects need to provide standard English version of the information.

    How important is after-sales service for mining gantry cranes?

    Brazilian mining losses are extremely high downtime, rapid troubleshooting, parts supply, technical maintenance guidance, is the key to protect the continuous production of the mine, perfect after-sales system is the core of long-term stable operation guarantee.

    MGB semi-gantry crane solution

    The MGB semi-gantry crane manufactured by Henan Mine Crane

    Summary

    The core of selecting a reliable Brazil mining and yard gantry crane supplier is not to find the lowest price, but to find a long-term partner who is suitable for the complex outdoor working conditions in Brazil, with excellent quality and perfect service.

    Brazilian mining areas are characterized by high temperature and rain, dust, salt spray corrosion in some areas, high frequency heavy-duty operations, ordinary general-purpose gantry cranes can not be adapted to long-term mass production needs. Only special equipment optimized for heavy-duty structure and upgraded outdoor protection can be adapted to the production rhythm of the local mining industry.

    High-quality gantry crane suppliers will provide professional support from the analysis of working conditions, model selection, program customization, quality control, factory inspection, delivery and installation, after-sales maintenance of the whole process, to help Brazilian mining projects to avoid purchasing mistakes, reduce the whole life cycle of operation and maintenance costs.

    Henan Mine Crane Industrial has been deeply engaged in the Brazilian mining lifting market for many years, and is familiar with the climatic conditions, site conditions and import acceptance standards of Brazilian mining areas, and has rich experience in overseas mining projects. We can customize all kinds of heavy-duty mining gantry cranes, provide exclusive anticorrosive, dustproof, windproof and waterproof upgraded configurations, with a full set of English compliance materials, remote technical guidance and long-term after-sales protection, is a reliable heavy lifting equipment partner for Brazilian mining and yard projects.

    Henan Mine CraneDiscuss your requirements ↗
  • Best Practices for Using Explosion Proof Electric Hoists

    Best Practices for Using Explosion Proof Electric Hoists

    Best Practices for Using Explosion Proof Electric Hoists

    Standard electrical equipment is one of the most common ignition sources in industrial fires and explosions. According to the U.S. Chemical Safety and Hazard Investigation Board (CSB), 281 combustible dust incidents occurred in American industry between 1980 and 2005, killing 119 workers and injuring 718 more. That single statistic explains why facilities in oil and gas, chemical processing, mining, and grain handling don’t use ordinary lifting equipment.

    An explosion proof electric hoist is built specifically to operate in these environments without becoming the spark that starts the next incident. But owning certified equipment is only half the job, using it correctly, every shift, is what actually keeps people safe. This guide covers the engineering behind explosion protection, the classification systems you need to understand, and the operational best practices that keep your hoist’s certification valid and your crew protected.

    What Is an Explosion Proof Electric Hoist?

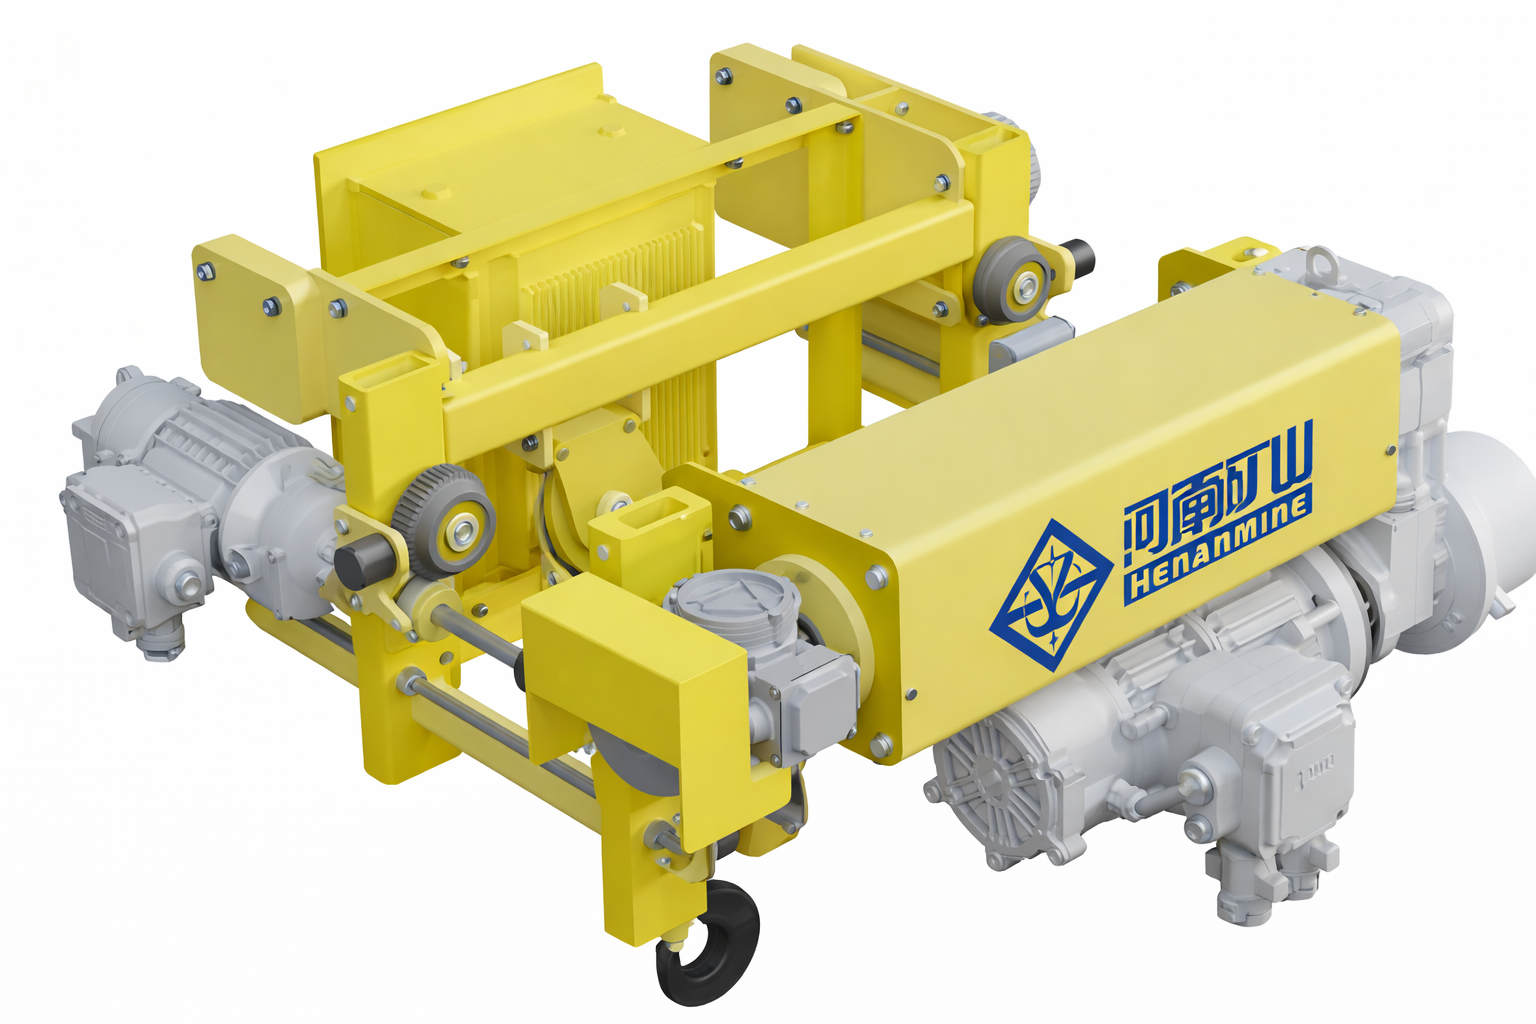
    Henan Mine Crane Factory supply explosion proof electric hoist is a lifting device engineered and certified to operate safely in locations where flammable gases, vapors, or combustible dust may be present in the air. It works by containing, limiting, or isolating any internal spark, arc, or hot surface so it can never reach the surrounding atmosphere. It matters because in a classified hazardous area, an ordinary hoist motor is a legitimate ignition risk, not a theoretical one.

    It’s worth clearing up a common misconception early: explosion proof does not mean blast resistant. The hoist isn’t designed to survive an external explosion. It’s designed so that it never causes one.

    Standard hoists fail this job in a few predictable ways: brush-type motors generate continuous sparking at the commutator, relay contacts arc every time they open or close, and surface temperatures on a hardworking motor can easily exceed the ignition temperature of common solvents or dusts. None of that matters in an open warehouse. All of it matters the moment flammable vapor or dust is in the air.

    These hoists typically use:

    • A flameproof or explosion-proof motor enclosure
    • An intrinsically safe or flameproof control box and pendant
    • Spark-free hardware on moving parts (wheels, hooks, trolleys)
    • Sealed cable entries and rigid conduit with seal fittings

    The 3 Engineering Principles Behind Explosion Protection

    Every certified explosion proof hoist relies on one or more of three core protection principles. Understanding them helps you evaluate whether a hoist actually fits your application — not just whether its spec sheet uses the right buzzwords.

    Principle How It Works Typical Component
    Confinement Contains an internal spark or explosion inside a flameproof enclosure so it can’t ignite the outside atmosphere Cast iron or aluminum flameproof motor and control box housings
    Energy Limitation Restricts electrical and thermal energy in the circuit below the level needed to ignite the atmosphere Intrinsically safe circuits and barriers
    Isolation Physically prevents hazardous gas or dust from reaching a potential ignition source Pressurization, purging, encapsulation, or sealed enclosures

    A well-built hoist often layers more than one principle. A flameproof motor (confinement) paired with an intrinsically safe remote control (energy limitation) is a common combination on modern units.

    It helps to see how this plays out in practice. A flameproof motor housing is machined with tight, specific clearances along every joint, if gas inside ever ignites, the flame front cools and loses energy passing through that narrow gap, so it never reaches open air. An intrinsically safe pendant, by contrast, doesn’t rely on a heavy enclosure at all. The circuit itself is designed so the maximum possible spark energy sits below what’s needed to ignite the specified gas group, even under a fault condition like a short circuit. Isolation methods show up less often on hoists themselves but are common on associated control panels, where purging the enclosure with clean air or nitrogen keeps hazardous atmosphere out entirely.

    Hazardous Area Classifications: ATEX, IECEx, NEC/CEC and GB3836

    Before you can apply any best practice, you need to know which classification system governs your facility. The four systems below cover most of the world, and they don’t always speak the same language.

    Standard Region Hazard Categories Example Marking
    ATEX (2014/34/EU) European Union Zones 0/1/2 (gas), Zones 20/21/22 (dust) Ex d IIB T4 Gb
    IECEx International Same zone system as ATEX Ex d IIC T4 Gb
    NEC/CEC United States/Canada Class I (gas) & Class II (dust), Division 1 or 2 Class I, Div 1, Group C
    GB3836 China Similar zone system, IEC-aligned with local requirements Ex d IIB T4

    A few terms you’ll see repeatedly on a hoist nameplate:

    • Gas Group (IIA/IIB/IIC):How easily the specific gas ignites. IIC is the most restrictive, covering gases like hydrogen.
    • Temperature Class (T1–T6):The maximum surface temperature the equipment is allowed to reach. T4, for example, caps surface temperature at 135°C.
    • Zone vs. Division:Zones (0/1/2) describe how often a hazardous atmosphere is present; Divisions (1/2) under NEC do the same with slightly different criteria.

    Beyond gas group and temperature class, the nameplate also specifies the protection method, the actual engineering technique used to prevent ignition. These appear as a letter code right after “Ex”:

    Code Protection Method How It Works
    Ex d Flameproof enclosure Contains any internal explosion; flame can’t escape through enclosure joints
    Ex e Increased safety Extra design margin against overheating and arcing, typically used on terminal boxes
    Ex i Intrinsic safety Limits electrical energy so a spark can never carry enough energy to ignite
    Ex p Pressurization Keeps a protective gas inside the enclosure at higher pressure than the surroundings
    Ex m Encapsulation Embeds electrical parts in a solid compound so gas or dust can’t reach them
    Ex n Non-sparking Built so normal operation produces no sparks; used in lower-risk Zone 2 areas

    Most explosion proof hoists combine Ex d on the motor and brake housing with Ex i on the control circuit, confinement for the high-power components, energy limitation for the low-power ones. Knowing this combination helps when you’re comparing two hoists with similar nameplate summaries but different underlying engineering.

    Henan Mine Crane Factory supply explosion proof electric hoist

    Explosion Proof vs. Weatherproof vs. Corrosion-Resistant: Don’t Confuse Your Ratings

    Procurement teams sometimes treat rugged industrial hoist specs as interchangeable, and that’s where mistakes start. These ratings solve completely different problems:

    • IP ratings (e.g., IP65, IP66)describe protection against dust and water ingress. A hoist can be IP66-rated and still have zero explosion protection, IP ratings say nothing about ignition prevention.
    • NEMA enclosure ratingsdescribe similar environmental protection in North American terms, again unrelated to hazardous-atmosphere certification.
    • Corrosion-resistant coatings or stainless constructionaddress chemical exposure and longevity, not spark or heat containment.
    • Ex/ATEX/IECEx/NEC hazardous-location ratingsare the only ones that actually address ignition risk in classified zones.

    A hoist can legitimately carry several of these ratings at once, for example, an offshore platform unit might need both an Ex d rating for the hazardous zone and a high IP rating for saltwater spray exposure. The mistake is assuming one substitutes for the other. If a spec sheet emphasizes rugged or weatherproof language without an explicit Ex/ATEX/IECEx marking and certificate number, it almost certainly isn’t rated for hazardous-area use.

    Industries That Require Explosion Proof Hoists

    Combustible dust and flammable gas hazards show up in more industries than most people expect. OSHA’s hazard guidance lists agriculture, chemicals, food production, grain handling, pharmaceuticals, metal processing, and fossil fuel power generation among the sectors at risk for dust-related fires and explosions.

    In practice, Henan Mine Crane Factory supply explosion proof hoists are standard equipment in:

    • Oil & gas and petrochemical facilities:Refineries, offshore platforms, and tank farms routinely classify entire process areas as Zone 1 or Zone 2 because of volatile hydrocarbon vapors.
    • Chemical manufacturing plants:Solvent handling, reactor loading, and drum transfer operations where flammable vapors can accumulate around fixed equipment.
    • Mining operations:Underground coal mines carry ongoing methane risk, while both underground and surface operations can see coal dust accumulate in confined areas.
    • Grain elevators and food processing:Flour, sugar, and grain dust create some of the most severe deflagration hazards in industry, since fine organic particulates ignite easily once suspended in air.
    • Pharmaceutical manufacturing:Flammable solvents used in tablet coating, extraction, and equipment cleaning processes.
    • Paint and coating lines:Spray booths can reach the lower explosive limit for airborne VOCs quickly in an enclosed space.

    If your facility has a documented hazardous area classification study covering any zone of your plant, that zone needs explosion proof lifting equipment, full stop.

    Best Practice 1: Select the Right Hoist for the Zone

    Selection mistakes are the root cause of most explosion-protection failures, because everything downstream depends on getting this step right. Use this checklist:

    1. Match zone, gas group, and temperature class exactly,don’t round up or assume a more protected rating automatically covers your application.
    2. Verify third-party certification documents, not just the marketing claim. The nameplate marking must match the certificate.
    3. Size for duty cycle, using FEM or CMAA duty classifications, not just maximum load capacity.
    4. Choose the right control method.A radio remote keeps the operator physically outside the hazardous zone, a pendant control needs to be rated for the same zone as the hoist itself.
    5. Never upgrade a standard hoistwith aftermarket explosion-proof parts. Certification applies to the complete assembly as tested, not to a kit bolted onto a non-rated unit.

    A quick reference for duty cycle classification:

    Classification System Light Duty Medium Duty Heavy Duty
    FEM 1Bm 2m 3m–4m
    CMAA Class A/B Class C Class D–F

    Choosing too light a duty class for actual usage shortens motor life and increases the chance of overheating, a real concern in a hazardous area, since surface temperature is part of what the certification depends on.

    New vs. Retrofitted Hoists: What the Standards Actually Allow

    Facilities under budget pressure sometimes ask whether an existing standard hoist can be converted for hazardous-area use instead of buying new. The honest answer: rarely, and not the way most people imagine it.

    Certification under ATEX, IECEx, or NEC applies to the complete assembly as tested in a lab, motor, enclosure, wiring, control box, and seals together. Swapping a standard hoist’s motor for a flameproof one doesn’t transfer the certificate, because the rest of the assembly, gearbox housing, terminal box, cable entries, was never tested as part of that protection system.

    What’s legitimate:

    • Buying a factory-built Henan Mine Crane manufacturedexplosion proof hoist from a manufacturer that holds the actual ATEX, IECEx, or NEC certificate for that specific model.
    • Retrofitting through the original manufacturer, if they offer an engineered retrofit kit that carries its own certification covering the modified assembly.
    • De-rating an existing hoist’s duty cycleto extend service life. This doesn’t change its hazard rating, but it’s a legitimate way to reduce thermal stress in borderline applications.

    What’s not legitimate, no matter how it’s marketed: bolting an explosion-proof motor onto a standard hoist frame and calling the result certified. If the paperwork doesn’t name your exact hoist model and serial range, the certification doesn’t apply to it.

    Best Practice 2: Install It to the Hazardous Area Drawing

    Installation in a classified area isn’t a general electrician’s job, it requires someone qualified in hazardous location wiring methods.

    • Install strictly according to your facility’s hazardous area classification drawing, not a generic layout.
    • Use rigid conduit with seal fittings at the required distance from the enclosure, per code, to prevent gas or flame propagation through the conduit run.
    • Bond and ground every component; static discharge is its own ignition risk independent of the electrical system.
    • Confirm ambient temperature and altitude derating,a hoist certified at sea level may need a different rating at higher elevation or temperature.
    • Run a full commissioning inspection before energizing the unit for the first time, and document it.

    Best Practice 3: Operate Within Strict Limits, Every Time

    Certified hardware doesn’t protect anyone if operating habits undermine it.

    • Run a pre-use visual and functional check before every shift,limit switches, hook, chain or rope condition, and unusual smells or discoloration.
    • Keep routine working loads at or below roughly 80% of rated capacity. This preserves thermal margin in the motor and reduces overheating risk.
    • Never bypass, wire around, or disable an overload limiter or limit switch, even temporarily. These devices exist specifically to prevent the shock loads and friction events that can generate sparks.
    • If the hoist shows abnormal heat, noise, or smell, stop operation immediately. Do not resume use until a qualified person identifies and corrects the cause.
    • Where possible, keep the operator outside the classified zone using a remote control rated for that purpose.

    Best Practice 4: Maintain and Inspect on a Documented Schedule

    Maintenance on explosion proof equipment carries a higher bar than standard hoists, because small errors here are what actually void certification.

    Frequency What to Check
    Daily (pre-shift) Visual inspection, functional test of brakes and limit switches, listen for abnormal sounds
    Monthly Hook and chain/rope wear, brake function, electrical connections, seal integrity
    Annual (qualified person) Flameproof joint surfaces, enclosure gaskets and IP ratings, torque specs on enclosure fasteners, full load test

    A few maintenance rules specific to hazardous-area equipment:

    • Only use OEM-certified replacement parts. Substitutions,even ones that look identical, can change clearances on flameproof joints by fractions of a millimeter, which is enough to void protection.
    • Never repaint, re-machine, or sand a flameproof joint surface without manufacturer guidance.
    • Keep written maintenance records. If certification is ever questioned, documentation is your proof of compliance.

    Documentation to keep on file for every unit:

    Document Purpose
    Original test certificate (ATEX/IECEx/NEC) Proves the as-built unit meets its claimed rating
    Installation commissioning report Confirms correct setup against the hazardous area drawing
    Inspection log (daily/monthly/annual) Demonstrates ongoing compliance and catches developing issues early
    Repair/parts replacement record Shows which parts were used and confirms they were OEM-certified
    Operator training records Confirms personnel were qualified to use the equipment

    In an audit, or after an incident, this paperwork is what separates a defensible safety program from a liability problem.

    Operator Training and Certification Requirements

    A hoist can be perfectly selected, installed, and maintained, and still cause an incident if the person operating it doesn’t understand why hazardous-area rules exist.

    Training should cover, at minimum:

    • How to read the hoist’s load chart and rated capacity, including why exceeding it even briefly compromises the thermal margins the certification relies on.
    • Pre-use inspection procedure and what to do if it fails,specifically, who to notify and how the unit gets tagged out of service.
    • Emergency stop procedures and lockout/tagout before any service work, including isolating power at the source rather than relying on the hoist’s own controls.
    • Why standard repair parts and field modifications are prohibited, framed around the actual mechanism (voided clearances, altered energy limits) rather than just company policy.
    • How to recognize signs of atmosphere changes,gas alarms, dust accumulation, unusual odors, relevant to the specific work area.

    Many facilities align refresher training with their annual equipment inspection cycle, so operators are re-evaluated on the same schedule the equipment is. This also gives new hires a natural touchpoint: pairing initial training with a walkthrough of the actual inspection log helps operators see how the daily checks they perform connect to the facility’s broader compliance record.

    Common Mistakes That Compromise Explosion Protection

    These are the failure points that show up again and again in field audits:

    1. Substituting non-certified hardware:Bolts, cable glands, or switches that aren’t part of the original certified assembly. Even a visually identical bolt can have different thread engagement that changes a flameproof joint’s tested clearance.
    2. Damaging flameproof joint surfaces:During cleaning, repainting, or repair. A scratch or extra coat of paint across a machined joint face can be enough to widen the gap beyond its certified tolerance.
    3. Mismatching gas group or temperature class:Using a T3-rated hoist where the area requires T4. This is most common when a hoist is moved from one part of a facility to another without re-checking the local classification.
    4. Skipping certificate verification at purchase:Trusting a marketing claim instead of the actual test certificate. “Explosion proof” on a product page isn’t the same as a certificate number you can verify with the issuing body.
    5. Letting untrained staff perform field fixes:On hazardous-area equipment. A well-intentioned quick repair by someone unfamiliar with hazardous-location rules is one of the most common ways certification gets quietly voided.
    6. Deferring maintenance:To cut costs or downtime, which is the single most common precursor to certification failure. Worn seals and degraded gaskets don’t announce themselves until they’ve already compromised protection.

    Why This Matters: The Cost of Getting It Wrong

    The numbers behind hazardous-area incidents make the case better than any sales pitch. The CSB’s review of U.S. industry found 281 combustible dust incidents between 1980 and 2005, with 119 deaths, 718 injuries, and extensive facility damage. OSHA’s own hazard communication guidance repeats this same data point because it remains the most cited baseline for the scale of the risk.

    OSHA’s hazardous locations standard (29 CFR 1910.307) and the National Electrical Code (NFPA 70) both exist because uncertified electrical equipment in a classified area isn’t a minor compliance gap, it’s a documented cause of fatal industrial accidents. Following the best practices above isn’t about checking a regulatory box. It’s about keeping your facility off that list.

    Beyond the human cost, the practical consequences compound quickly. An OSHA citation for using or maintaining uncertified equipment in a classified location can trigger a broader facility-wide audit, not just a fine for the one piece of equipment in question. Insurance carriers frequently treat documented hazardous-area compliance as a condition of coverage, so a voided certification discovered after an incident can affect a claim. And unplanned downtime to replace or re-certify equipment after the fact almost always costs more than the original price difference between standard and certified hoists would have.

    Frequently Asked Questions

    Q: What does “explosion proof” actually mean on a hoist nameplate?

    It means the hoist has been independently tested and certified to prevent internal sparks, arcs, or excess heat from igniting the flammable gases, vapors, or combustible dust in the area where it’s installed. The nameplate marking (e.g., Ex d IIB T4) specifies the exact protection method, gas group, and temperature class it’s rated for.

    Q: What’s the difference between ATEX and IECEx certification?

    ATEX is a European Union directive (2014/34/EU) that’s legally mandatory for equipment sold or used in the EU. IECEx is a global certification scheme administered by the International Electrotechnical Commission, used to simplify cross-border trade outside Europe. Both use similar zone, gas group, and temperature class systems, but they are separate certifications with separate paperwork.

    Q: Can I use a Class I Division 1 rated hoist in a Class II (dust) location?

    No. Class I covers flammable gases and vapors, while Class II covers combustible dust, and the protection methods differ. A hoist rated only for Class I gas groups has not been tested or certified for dust ignition risks, so using it in a dust environment voids its protection and creates a real hazard.

    Q: How often should an explosion proof hoist be inspected?

    Most facilities run a daily pre-shift visual and functional check, a documented monthly inspection of wear items like hooks, brakes, and limit switches, and a thorough annual inspection by a qualified person that includes checking flameproof joint surfaces and enclosure seals. Always follow the manufacturer’s specific schedule, since it can be stricter than general industry practice.

    Q: What voids the explosion-proof certification of a hoist?

    Common causes include installing non-certified replacement parts, damaging or re-machining flameproof joint surfaces during repair, painting over enclosure gaps, drilling unauthorized holes, or making any modification not covered by the original certificate. Once voided, the hoist must be re-certified before returning to service in a hazardous area.

    Q: Do explosion proof hoists cost more than standard hoists?

    Yes, typically more upfront due to specialized motors, flameproof enclosures, and third-party certification testing. However, the higher initial cost is generally offset over time by reduced accident risk, lower insurance and liability exposure, and avoidance of regulatory penalties for using uncertified equipment in a classified area.

    Q: How long do explosion proof hoists typically last?

    With proper maintenance, most explosion proof hoists run 15-20 years or more, similar to standard industrial hoists. The certified components don’t inherently wear out faster than standard equivalents, what shortens service life is usually deferred maintenance or running the unit consistently above its rated duty cycle, not the explosion-proof rating itself.

    Q: Who is qualified to repair or service an explosion proof hoist?

    Repairs should be performed by technicians trained specifically in hazardous-area equipment, ideally through the original manufacturer or an authorized service partner. A general industrial electrician without hazardous-location training can unintentionally void certification, even while performing what looks like routine maintenance.

    Henan Mine Crane Factory Custom

    Safe explosion protection begins well before the first lift. Selecting an explosion proof electric hoist that is suitable to your hazardous area rating, duty cycle and operating environment minimizes the compliance issues, increases plant safety and ultimately provides a satisfactory return on investment for many years of service. In conjunction with proper installation, periodic inspections and preventative maintenance, an optimal piece of equipment will provide a dependable service life in a harsh industrial environment.

    As a long trusted manufacturer of explosion proof lifting equipment, we can offer of tailored solutions for oil and gas, chemical industries, storage, mining, offshore and many other hazardous industries.Whether you are starting a new project, replacing an existing hoist, or upgrading inefficient rigging equipment, our team of engineers can assist you select the perfect explosion proof electric hoist to meet your lifting capacity, application environment and duty cycle-and ensure a safe, reliable and economically built-piece of equipment for years to come.

    Henan Mine CraneDiscuss your requirements ↗
  • Automotive Manufacturing Cranes: Improving Factory Efficiency

    Automotive Manufacturing Cranes: Improving Factory Efficiency

    Automotive Manufacturing Cranes: Improving Factory Efficiency

    In the modern intelligent automobile manufacturing system, production efficiency, operation safety, and process stability are the three keys for automobile companies to enhance their core competitiveness.Automobile manufacturing belongs to a heavy-duty, continuous, and high-precision production industry. From stamping sheet metal and powertrain processing to vehicle assembly and equipment operation and maintenance, the whole process involves a large number of heavy-duty parts handling, precision hoisting and equipment shifting operations.As the core material handling and production supporting equipment of the factory, Automotive Manufacturing Crane has long replaced traditional manual handling and simple hoisting equipment, and has become the core equipment for car companies to reduce costs and increase efficiency, avoid safety risks, and ensure the uninterrupted operation of assembly lines.

    Why Automotive Factories Need Heavy-Duty Cranes

    Automobile manufacturing is different from ordinary light industrial manufacturing. It has the characteristics of large loads, dense processes, strong continuity, high accuracy requirements, and strict safety standards. Traditional handling equipment is completely unable to adapt to large-scale and intelligent automobile production models.Relying on the advantages of large load, high stability, high precision, and continuous operation, heavy-duty industrial cranes have become just-needed supporting equipment for automobile factories, and their core values are reflected in three dimensions.

    Moving heavy automotive components

    The whole process of automobile production is filled with all kinds of heavy-duty parts, covering large-scale body sheet metal parts after stamping, engine blocks weighing several tons, transmission assemblies, chassis frames, battery packs (new energy vehicles) and other core components.The weight of such parts ranges from hundreds of kilograms to tens of tons, and manual handling is completely impossible. Ordinary forklifts and simple cranes not only have insufficient loads, but they are also prone to problems such as shaking, offset, and collision damage of parts.Henan Mine Crane manufactured special crane for heavy-duty vehicle manufacturing can smoothly lift and accurately shift all kinds of heavy-duty auto parts, without bumps and offsets throughout the process, to maximize the protection of the integrity of high-precision auto parts, greatly reduce the scrap rate of parts, and control production costs from the source.

    Supporting continuous production

    Modern automobile factories adopt a closed-loop production model of assembly lines. The processes of stamping, welding, coating, assembly, and powertrain production are interlocking. Any one link is stuck or shut down, which will cause the entire production line to stagnate and bring huge production capacity losses.Henan Mine Crane manufactured heavy-duty cranes can realize the rapid transfer and precise docking of parts and production equipment, ensure the timely supply of materials in each process, and avoid problems such as material accumulation and downtime due to lack of materials.At the same time, key processes such as equipment failure emergency repair, mold replacement, and production line commissioning all rely on cranes to complete operations quickly, minimize production line downtime, and support the factory’s 24-hour uninterrupted, high-load continuous production, effectively improving the overall production capacity utilization rate.

    Improving workplace safety

    Heavy-duty material handling in automobile factories is a high-risk operation scenario. Manual assisted handling and simple equipment hoisting can easily cause safety accidents such as heavy objects falling, personnel squeezing, and parts dumping, which not only threaten the personal safety of operators, but also cause equipment damage, production interruption and other secondary losses.Our heavy-duty industrial cranes are equipped with multiple safety protection systems such as overload protection, limit braking, anti-shake control, and emergency shutdown. Mechanized and automated hoisting operations are realized throughout the process, greatly reducing manual intervention in high-risk operations.The standardized lifting operation mode can thoroughly standardize the material handling process of the factory, reduce the rate of work-related accidents and compliance risks, help car companies meet industrial safety production standards, and create a safe, stable and compliant production and operating environment.

    Where Cranes Are Used in Automotive Manufacturing

    Cranes run through the entire production chain of automobile manufacturing, covering the core production workshop, equipment operation and maintenance, warehousing and logistics and other scenarios. They are adapted to different types of lifting equipment under different working conditions and accurately match the operating needs of all aspects of automobile manufacturing. It is an indispensable core equipment for the whole process of production.

    Stamping and body shops

    The stamping workshop and the body workshop are the front-end core workshops of automobile production. They are mainly responsible for automobile sheet metal stamping, body welding, and body forming operations. The core high-frequency operations are large-scale stamping die replacement, heavy-duty sheet metal parts hoisting and transferring, and body frame shifting and positioning.A single set of stamping dies can weigh up to tens of tons, with high replacement frequency and high accuracy requirements. Special bridge cranes can quickly complete the lifting, shifting, and precise alignment of the molds, greatly shortening the mold replacement and debugging time.At the same time, it can smoothly transfer sheet metal parts such as large doors, roof tops, and body panels to avoid sheet metal deformation and scratches, ensure the machining accuracy of the body, and adapt to the high-frequency, heavy-duty, and high-precision operations of stamping and body workshops.

    Engine and powertrain production

    Powertrain components such as engines, gearboxes, and drive shafts are the core precision components of automobiles, which have the characteristics of high weight, high precision, and easy damage.In the powertrain production workshop, cranes are mainly used for hoisting blank castings, transshipment of semi-finished products, assembly alignment of finished products, loading and unloading of precision processing equipment, etc.With the help of the crane’s smooth start-stop and precise positioning functions, the non-destructive handling and assembly of precision power components can be realized, component wear and assembly deviations caused by manual operation can be effectively avoided, the yield rate of powertrain products can be improved, and the production quality of core components can be guaranteed. Stability.

    Assembly lines

    The complicated process and large material flow in the vehicle assembly workshop are one of the most widely used scenarios for cranes.During the assembly process, it is necessary to complete the lifting of large-scale components such as engine assembly, chassis assembly, battery pack, and cockpit assembly through lifting equipment, and accurately assemble and align them.Light-duty lifting equipment and electric hoists adapted to assembly line operations can realize lightweight and high-frequency hoisting operations, and operate synchronously with the beat of the production line to achieve on-demand and precise docking of materials, completely solve the problems of material accumulation, low assembly efficiency, and poor alignment accuracy in the assembly process, and greatly improve the efficiency and standardization of vehicle assembly.

    Maintenance and equipment handling

    All kinds of large-scale production equipment, stamping machine tools, welding equipment, and automated assembly line equipment in automobile factories are large in size and heavy in weight, making it extremely difficult to install, overhaul, replace, and relocate equipment.Henan Mine Crane manufactured cranes can efficiently complete the lifting and shifting of large-scale production equipment, disassembly, assembly and maintenance, component replacement and other operations, quickly deal with equipment failures, and complete the transformation and upgrading of production lines.Compared with manual disassembly and assembly and simple hoisting, professional lifting equipment can significantly shorten the operation and maintenance time of equipment, reduce the loss of equipment disassembly and assembly, ensure the stable operation of various production equipment in the factory, and reduce the loss of production capacity caused by equipment failures.

    Warehousing and material storage

    The storage and transportation of finished parts, large molds, spare equipment, and heavy raw materials in automobile factories is also inseparable from lifting equipment.Heavy-duty material stacking, warehousing, and shift sorting operations in the workshop storage area and material stacking area can be standardized and efficient material transfer through cranes, which can solve the problems of manual handling of heavy materials, chaotic stacking, and low warehousing efficiency, optimize the utilization rate of storage space, standardize material management processes, ensure efficient turnover of production materials, and provide guarantees for continuous feeding of production lines.

    How Cranes Improve Automotive Factory Efficiency

    For large-scale automobile manufacturing enterprises, the improvement of production efficiency is essentially the comprehensive result of process optimization, manpower reduction, loss reduction, and downtime reduction.Professional automobile manufacturing cranes enable factories to improve quality and efficiency in all directions from the four dimensions of material handling, production process, labor cost, and equipment operation and maintenance, and help automobile companies achieve cost reduction and efficiency, and upgrade production capacity.

    Reduce material handling time

    The traditional manual handling mode with simple equipment, a single heavy-duty material transfer takes a long time, the process is cumbersome, and it is prone to problems such as material waiting and transportation stuck, which seriously slows down the overall production beat.Special-purpose truck cranes have the advantages of fast start and stop, wide-range coverage, and continuous operation. They can realize the rapid transfer of heavy materials across regions and large quantities, and the efficiency of single hoisting and transfer is increased by more than several times.At the same time, intelligent lifting equipment can accurately locate the material point, reduce the invalid and time-consuming repeated adjustment and alignment, and greatly compress the material turnover cycle, allowing the efficient flow of raw materials, semi-finished products, and finished products, and speed up the entire production link from the material port.

    Improve production workflow

    Automobile assembly line production has extremely high requirements for process coherence and matching, and the rhythm of material handling directly determines the rhythm of production line production.Customized lifting equipment can be fully adapted to the production processes of each workshop of the automobile factory, matching the operation beats of different links such as stamping, processing, assembly, warehousing, etc., to form a standardized and integrated material handling process.Through accurate material supply, mold switching, and equipment matching, pain points such as material disconnection, process waiting, and process faults in traditional production are completely solved, so that all production links are seamlessly connected, and the overall production workflow is optimized to achieve full load, standardized and efficient operation of the assembly line.

    Minimize manual handling

    Traditional heavy-duty material handling requires multiple workers to work together, high labor costs, high labor intensity, and high manual operation error rate, which can easily cause material damage and operational errors.Modern automobile manufacturing cranes realize the whole process of mechanization and automation, greatly reducing manual participation in high-risk physical work such as heavy handling, hoisting, and alignment.Enterprises can streamline redundant handling manpower, allocate human resources to core positions such as precision assembly, quality inspection, and equipment operation and maintenance, optimize the manpower allocation structure, and completely avoid material losses and operational errors caused by manual operations, and reduce production fault tolerance costs.

    Speed up equipment maintenance

    The operation and maintenance efficiency of automobile factory automation equipment and large machine tools directly determines the effective production time of the factory.In the absence of professional lifting equipment, large-scale equipment disassembly, component replacement, and mold debugging take a long time, and long-term downtime will cause huge production capacity losses.High-performance industrial cranes can quickly complete the hoisting, shifting, disassembly, and resetting of large-scale equipment, greatly shorten the construction period of equipment overhaul, maintenance, and replacement, and quickly resume production line production.Normalized and efficient equipment operation and maintenance can effectively improve the equipment start-up rate, reduce the length of invalid downtime, and maximize the release of factory production capacity.

    Which Cranes Are Suitable for Automotive Factories

    The working conditions of automobile manufacturing are diverse and the load span varies greatly. Different workshops and processes have different requirements for the load, span, and operating mode of the crane.In view of the refined and differentiated operation needs of automobile factories, the mainstream adaptation models in the industry are divided into four categories, accurately covering all working conditions such as light load, indoor and outdoor, and high frequency.

    Overhead cranes for production areas

    Henan Mine Crane manufactured bridge crane is the main model of automobile production workshop, widely used in stamping workshop, assembly workshop, powertrain workshop and other indoor core production areas.This type of crane is erected on the top of the plant, does not occupy ground production space, has a wide operating coverage, stable operation, and high positioning accuracy, and can be adapted to high-frequency and continuous production line hoisting operations.Whether it is large-scale mold replacement, body parts transfer, or assembly parts assembly alignment, bridge cranes can output stably and are perfectly adapted to the needs of large-scale and standardized production operations in automobile factories. It is the core lifting equipment with the highest penetration rate of automobile companies.

    automotive factory cranes

    Gantry cranes for outdoor handling

    Gantry cranes are mainly suitable for outdoor working conditions such as outdoor depots, outdoor storage, and equipment transfer in automobile factories.The outdoor stacking and transportation of large spare equipment, giant molds, bulk raw materials, and finished vehicle accessories in automobile factories can all be completed by gantry cranes.The equipment is highly adaptable to the site, does not need to rely on the plant structure, has strong stability in open-air operations, good wind resistance, and flexible load span. It can meet the outdoor hoisting and transportation needs of large-volume and heavy-weight materials, and make up for the shortcomings of outdoor material handling equipment in automobile factories.

    Electric hoists for lighter loads

    Electric hoists are light-duty lifting equipment, mainly for light-load, high-frequency, and small-range precision hoisting, and are widely used in assembly lines, precision parts processing workshops and other scenes.For the hoisting and shifting operations of small and medium-sized precision parts, tooling fixtures, and small equipment components of automobiles, the electric hoist is small in size, stable in start and stop, flexible in control, and accurate in positioning. It can perfectly match the refined operation beat of the assembly line, make up for the lack of flexibility in small-load operations of large cranes, and achieve full coverage of light and heavy working conditions.

    Double girder cranes for heavy components

    Double-girder bridge crane is a special model for heavy-duty working conditions. It is specially designed for large-weight and ultra-high-precision hoisting operations in automobile factories. It is mainly suitable for the handling and installation of heavy-duty components such as heavy-duty stamping molds, large machine tools and equipment, giant chassis assemblies, and new energy heavy-duty battery modules.Compared with single-girder cranes, double-girder models have stronger carrying capacity, more stable structure, and better fatigue resistance. They can adapt to high-load and uninterrupted heavy-duty operations for a long time. There is no shaking in hoisting and higher alignment accuracy, which effectively guarantees the stability of the production and operation and maintenance of heavy-duty core components.

    Key Factors When Choosing an Automotive Manufacturing Crane

    Henan Mine Crane manufactured automobile manufacturing cranes belong to the core industrial production equipment, and the selection directly affects production efficiency, operation safety and equipment service life.Car companies cannot blindly benchmark general-purpose models in the selection of models. They need to consider their own production conditions, workshop layout, and production beats comprehensively, focusing on the six core parameters, and accurately matching and adapting equipment.

    Lifting capacity

    The rated lifting weight is the core basic parameter of the selection, and it must strictly match the maximum lifting load of the factory.Car companies need to determine the crane load based on the maximum mold weight, the heaviest parts, and the maximum equipment weight in the workshop, and at the same time reserve a safety margin of 10%-20% to avoid full load and overload operations.Light-duty assembly workshops can choose small-tonnage equipment, and stamping and heavy-duty equipment operation and maintenance workshops must match large-tonnage double-girder cranes to eliminate equipment failures, safety hazards and production capacity constraints caused by insufficient loads.

    Span and lifting height

    The span and lifting height of the crane need to be adapted to the building parameters and operating range of the plant.It is necessary to determine the effective span of the crane based on the width of the workshop and the spacing of the columns to ensure that there are no dead ends in the operation.At the same time, the lifting height is determined according to the installation height of the equipment, the height of the material stacking, and the height of the assembly operation to ensure that heavy materials can be hoisted, shifted, and aligned smoothly, so as to avoid space constraints that the operation cannot be carried out, and it is fully adapted to the three-dimensional working space of the workshop.

    Working class and duty cycle

    Automobile factories are mostly continuously produced for 24 hours a day. Lifting equipment is high-frequency and long-working equipment. The working level and working system directly determine the durability and service life of the equipment.In high-frequency operation scenarios such as stamping workshops and assembly workshops, Henan Mine Crane manufactured industrial-grade cranes with high work-level and high load continuity rates need to be selected, which can adapt to long-term continuous start-stop and repeated hoisting operations to avoid aging, failure, caton and other problems in long-term high-load operation of ordinary models, and ensure long-term stable operation of equipment.

    Travel speed and positioning accuracy

    Automobile precision parts assembly, mold alignment, and assembly line supporting operations have extremely high accuracy requirements.The operating speed of the crane needs to take into account efficiency and stability, start and stop smoothly without impact, and avoid material shaking and offset caused by excessive speed.At the same time, it is necessary to have high-precision positioning capabilities to meet the needs of millimeter-level alignment, adapt to the assembly of precision parts and the precise installation of molds, not only to ensure production efficiency, but also strictly control production accuracy and product yield.

    Factory layout

    The workshop layout, space structure, and production line layout of different car companies vary greatly.The space of the old factory building is compact and the columns are dense, so lightweight and compact lifting equipment needs to be selected.The newly built intelligent factory building has a wide space and a high degree of automation, and can be equipped with large-span, intelligent, and linkage lifting equipment.The selection needs to be fully adapted to the structure of the plant, the ground space, and the layout of the production line, avoid interference between the equipment and the plant and the assembly line, maximize the use of the three-dimensional space of the workshop, and do not occupy the core production operation area.

    How to Customize Cranes for Automotive Production

    Standardized general-purpose cranes cannot be fully adapted to the personalized and refined production needs of automobile manufacturing. Customized lifting equipment has become the mainstream choice for modern automobile intelligent manufacturing.Exclusive customization is carried out according to the production process, workshop conditions, and future production capacity planning of automobile companies, which can maximize the efficiency of equipment and fit the exclusive production model of the enterprise.

    Match the crane to production processes

    The core of customized design is process adaptation, and exclusive equipment parameters are customized for the operating characteristics of different production processes.According to the high-frequency mold replacement conditions in the stamping workshop, optimize the operating speed and braking system of the equipment to improve the efficiency of mold replacement.According to the precision assembly conditions of the powertrain, the anti-shake and precise positioning system is upgraded to ensure the assembly accuracy.According to the storage and transshipment conditions, optimize the continuous operation capacity, improve the efficiency of material turnover, and make each crane accurately match the corresponding production process.

    Adapt to limited factory space

    For the pain points of small space, dense columns, low altitude and high altitude in old factories, space adaptation can be customized.By optimizing the main beam structure, end beam size, and walking mechanism of the crane, a compact customized model is created to adapt to small space operations without changing the structure of the plant.At the same time, optimize the operation schedule, avoid interference with columns, equipment, and pipelines, maximize the use of the limited three-dimensional space of the workshop, and solve the problem of upgrading the equipment of the old plant.

    Configure lifting and control options

    Combined with the needs of intelligent automobile production, the hoisting configuration and control system can be customized on demand.Intelligent anti-shake system, precise positioning system, frequency conversion speed control system, and remote control system can be installed to meet the needs of precision and efficient operations.Strengthen the load-bearing structure and braking system for heavy-duty working conditions.Optimize the motor and transmission structure for high-frequency operations, and upgrade the durability of the equipment.At the same time, it can be used with wireless remote control, ground operation, and air operation control modes to adapt to different operating scenarios and improve operation convenience and safety.

    Plan for future production needs

    High-quality customized solutions for automobile manufacturing cranes, taking into account the current needs of use and future production capacity upgrades.Reserve upgrade space in the design of equipment load, span, and operating performance to adapt to the production needs of enterprises’ subsequent capacity expansion, production line transformation, and product iteration (such as the transformation of traditional fuel vehicles to new energy vehicles).Avoid short-term equipment elimination and repeated procurement, reduce the iteration cost of enterprise equipment, and enhance the long-term use value of equipment.

    Henan Mine Crane Factory Custom

    Henan Mine Crane Factory supply special crane for automobile manufacturing is deeply adapted to the whole scene of stamping, assembly, powertrain production and equipment operation and maintenance of automobile companies, and accurately solves the core pain points such as difficult handling of heavy objects, low efficiency, and large safety risks in factories.Relying on the core advantages of heavy-duty stability, high-precision positioning, and customizable plant layout, the production process is effectively optimized, the material turnover time is shortened, and the labor and operation and maintenance costs are reduced.Deeply engaged in the field of lifting equipment manufacturing, Henan Mine Crane Factory can be customized according to the production capacity planning of car companies and workshop working conditions, helping car companies to achieve intelligent manufacturing upgrades, efficient and stable production, cost reduction and efficiency.

    Henan Mine CraneDiscuss your requirements ↗
  • Automated RTG Crane: The Future of Smart Container Terminal Operations

    Automated RTG Crane: The Future of Smart Container Terminal Operations

    Automated RTG Crane: The Future of Smart Container Terminal Operations

    Under the tide of intelligent transformation of global ports, the pain points of traditional container terminals relying on manual operation, limited efficiency, many potential safety hazards and high operation costs are increasingly prominent, which cannot meet the industrial demand of rapid development of cross-border logistics and increasing container throughput year by year.With the core advantages of high-precision operation, unmanned operation and intelligent dispatching coordination, the Automated RTG Crane has completely reconstructed the operation mode of container yard and become the core standard equipment for upgrading modern intelligent ports and intelligent logistics hubs.This article will completely disassemble the automatic RTG crane, providing professional and comprehensive selection and upgrading reference for the purchaser.

    What Is an Automated RTG Crane?

    Definition of automated RTG crane

    Henan Mine Crane manufactured automatic RTG crane, full name of automatic tire gantry crane, is a modern port-specific lifting equipment equipped with intelligent control system, high-precision positioning module, vision recognition system and autonomous anti-shake technology. It is an intelligent upgrade iteration product of traditional tire gantry crane.Different from fixed rail cranes, this equipment adopts rubber tire walking structure, without laying fixed rails, can move flexibly in hardened sites, and adapts to the flexible operation requirements of multi-area and multi-station container yards.

    The core of the equipment relies on the terminal operating system (TOS) and the equipment control system (ECS) to cooperate and link together. Through multi-sensor fusion sensing and intelligent algorithm scheduling, the equipment can independently complete the whole process operations such as container grabbing, handling, stacking, alignment and dropping. It does not need manual real-time control and can operate stably 24 hours a day. It is the core main equipment for intelligent container terminal yard operation and is widely used in port yard, logistics hub, freight terminal and other scenarios.

    Automated vs traditional RTG crane

    The core operational differences between automated RTG cranes and traditional RTG cranes can be clearly compared in the following table, covering key operational indicators:

    Comparison Item Traditional RTG Automated RTG
    Operation Mode Full manual cab operation Unmanned automatic + remote control
    Operation Accuracy Large alignment errors, irregular stacking MM-level precision, zero manual errors
    Working Efficiency Unstable, limited by labor and weather 24/7 stable and high-efficiency operation
    Safety Level High risk of on-site accidents Zero on-site personnel safety risks
    Operating Cost


    High labor and management costs Greatly reduced labor and energy costs
    Management Empirical and extensive management Standardized and digital management

    How Does an Automated RTG Crane Work?

    Control system

    The control system is the core brain of the automated RTG crane. It adopts PLC industrial control + edge computing three-level architecture and is equipped with exclusive equipment control programs to realize instruction issuance, logic operation, status control and fault warning of the whole operation process.The system can seamlessly connect the port TOS terminal operating system and ECS equipment management and control system, receive the yard operation task list in real time, automatically disassemble the operation steps, plan the optimal operation path, and coordinate all actions such as equipment walking, lifting, amplitude variation and rotation.

    Compared with the traditional single control mode, the automatic control system has millisecond command response speed, can adjust the equipment operation parameters in real time, adapt to the operation requirements of different specifications and different weight containers, and has the data storage, operation traceability and parameter adaptive adjustment capabilities to ensure the long-term stable and standardized operation of the equipment, effectively avoiding the arbitrariness and non-standardization of manual operation.

    GPS positioning

    Henan Mine Crane manufactured automatic RTG is equipped with high-precision Beidou +GPS dual-mode positioning system, integrating UWB ultra-wideband positioning module and inertial navigation unit to realize accurate positioning at millimeter level in the whole yard, with positioning accuracy up to ±10mm, completely solving the problems of large alignment deviation, irregular stacking and low site utilization rate of traditional equipment.The system can collect real-time equipment position, operation track and operation coordinate data, and independently plan the optimal walking route and operation point by combining with the electronic map of the yard.

    During the operation process, the positioning system dynamically calibrates the posture of the equipment in real time, corrects the walking offset and position deviation in time, ensures that each container grabbing, dropping and stacking accurately conforms to the preset coordinates, not only improves the operation accuracy, but also maximizes the utilization of the yard space, improves the container stacking density, and effectively improves the overall storage capacity utilization rate of the port yard.

    Container recognition

    The equipment is equipped with 3D vision recognition system and laser scanning perception module, combined with deep learning algorithm to realize full-dimensional intelligent recognition of containers.During the operation process, the vision system can quickly and accurately identify the size, specification, box number, posture and placement angle of the container, and detect the damage, lock hole position, box offset and other conditions of the container in real time, so as to provide accurate data support for the grasping operation.

    Compared with manual naked eye recognition, the intelligent identification system is not affected by light, weather and day and night environment, and the identification accuracy rate is close to 100%. It can quickly adapt to the operation requirements of various standard containers such as 20 feet, 40 feet and 45 feet. At the same time, it can accurately identify obstacles, vehicles and personnel in the yard, providing core perception support for equipment collision avoidance and safe operation, and avoiding misoperation risks from the technical level.

    Smart Port

    Anti-sway control

    In container lifting operation, the sloshing of spreader and container body is the core problem that affects the operation precision, slows down the operation efficiency and causes the safety hidden danger.The automatic RTG is equipped with an intelligent anti-sway control system, which monitors the swing amplitude, frequency and direction of the spreader in real time through dynamic algorithms, and outputs damping adjustment instructions in real time in combination with the running speed and working height of the equipment.

    The system can actively suppress the swing of the box during the whole process of equipment walking, lifting and braking, quickly eliminate the operation shaking, realize stable lifting and stable falling without manual intervention, greatly shorten the waiting time for single operation to stabilize the box, improve the operation cycle efficiency, effectively reduce the risk of collision, falling and damage of the box, ensure the safety of container operation and reduce the loss of goods.

    Remote operation

    Automatic RTG supports remote centralized control and unmanned autonomous operation mode, equipped with remote control console, operators can leave the site high-risk operation environment, in the central control room to complete remote monitoring, command scheduling and abnormal intervention of multiple equipment.Relying on the high-speed communication network, the equipment operation screen, operation data and equipment status can be synchronized to the central control platform in real time to realize visual remote control.

    Key Technologies Behind Smart RTG Crane Automation

    Artificial intelligence

    Artificial intelligence is the core support for intelligent RTG crane to realize high-level automatic operation. The equipment is equipped with three AI core algorithms: deep learning, autonomous decision-making and intelligent scheduling.AI algorithm can independently optimize operation path, stacking logic and scheduling scheme through mass operation data training, dynamically adjust operation plan according to arrival and departure frequency, stacking status and operation priority of container yard, and realize optimal allocation of yard resources.

    At the same time, AI system has the ability of independent error correction and self-adaptation of working conditions, which can accurately identify unconventional operation scenarios and slight abnormalities of equipment, and adjust operation parameters independently without manual frequent debugging.Compared with traditional fixed-procedure operation equipment, AI-enabled automated RTG operation efficiency has been improved by more than 30%, operation fault tolerance rate and intelligent level have been greatly upgraded, and it is suitable for complex and changeable port operation scenarios.

    IoT monitoring

    The IoT monitoring system realizes automatic RTG full-equipment, full-working condition and full-time data acquisition and status monitoring.The equipment is equipped with multi-dimensional sensors such as temperature, vibration, speed, pressure, energy consumption and position, which collect equipment operating parameters, operation data, energy consumption data and fault information in real time and transmit them to the cloud management and control platform through the Internet of Things.

    Management personnel can view the operation status, operation output, energy consumption and equipment working conditions of each RTG in real time through terminal equipment, realizing equipment visualization and digital control.At the same time, IoT system can automatically count operation data, generate operation reports, accurately record container operation volume, operation duration and energy consumption loss, provide accurate data support for port operation optimization, equipment maintenance and cost accounting, and completely change the extensive management mode of traditional manual statistics.

    Digital twin

    Digital twin technology provides core enabling for intelligent operation and maintenance and scheduling upgrade of automated RTG. By constructing 1:1 virtual simulation model of equipment and yard operation scenario, real-time data synchronization and state linkage between physical equipment and virtual model are realized.The system can simulate equipment operation track, operation process and storage yard storage state in real time, and predict operation conflict, equipment hidden danger, site congestion and other problems in advance.

    Relying on the digital twin simulation capability, the port can simulate the operation scheme in advance, optimize the dispatching logic, predict the equipment maintenance cycle, complete the scheme debugging and parameter optimization without shutdown, and greatly reduce the trial and error cost.At the same time, it can realize visual traceability of equipment faults, quickly locate fault points and causes, improve operation and maintenance efficiency, and ensure high-load, uninterrupted and stable operation of equipment.

    5G communication

    5G communication technology is the network foundation of automatic RTG efficient coordination, remote control and real-time data transmission. It has the core advantages of low delay, high bandwidth, large capacity and anti-interference, which perfectly meets the communication requirements of complex port operation environment.Compared with 4G and traditional wireless communication mode, 5G network delay is reduced to millisecond level, which can guarantee real-time synchronous transmission of equipment control instructions, video pictures and sensing data, and eliminate problems such as command delay, picture jam and data loss.

    Relying on 5G technology, multiple automatic RTG can realize cluster collaborative operation, real-time linkage with AGV unmanned transport vehicle, port dispatching system, access control system and monitoring system, build intelligent operation system with global coordination, realize seamless connection of port operation process, greatly improve overall operation circulation efficiency, and is the core communication guarantee for all-unmanned intelligent port construction.

    Fault diagnosis

    Automatic RTG is equipped with intelligent fault diagnosis and early warning system, relying on big data analysis and AI algorithm to realize independent detection, accurate positioning, early warning and intelligent traceability of equipment faults.The system monitors the operating parameters of core components such as motor, hydraulic system, control system, positioning module and sensing equipment in real time, compares the standard operating condition data, and timely identifies abnormal fluctuations.

    For minor faults, the system can automatically complete fault repair and parameter calibration.For major faults, sound and light early warning can be issued in real time, and fault points, fault causes and solutions can be pushed to operation and maintenance terminals synchronously to avoid safety accidents and equipment damage caused by equipment operation with faults.This technology greatly reduces the failure rate of equipment, prolongs the service life of equipment, shortens the downtime and maintenance time, and ensures the continuity of port operations.

    Benefits of Automated RTG Cranes in Container Terminal Operations

    Higher efficiency

    Automatic RTG completely breaks the efficiency bottleneck of manual operation and realizes leapfrog improvement of port operation efficiency.The equipment can operate continuously for 24 hours without interruption, without efficiency interruption caused by manual rest, shift change and fatigue operation, stable operation rhythm and faster circulation speed.Relying on AI intelligent dispatching and optimal path planning, redundant operations such as invalid walking, repeated alignment and container stabilization waiting are reduced, and the cycle time of single container operation is greatly shortened.

    The measured data shows that the operation efficiency of automatic RTG is 40%-60% higher than that of traditional manual equipment, and the daily operation volume of single equipment is increased by more than 50%. The coordinated operation of multi-equipment cluster can greatly improve the overall throughput of the port, effectively solve the problems of container accumulation and inbound and outbound congestion in the port, and meet the needs of large-scale and efficient development of cross-border logistics.At the same time, standardized automatic operation can improve the regularity of storage yard and improve the site utilization rate by more than 15%.

    Improved safety

    Safety is the core bottom line of port terminal operation. Automatic RTG reconstructs port safety operation system from the source to avoid potential safety hazards of traditional operation in an all-round way.Traditional RTG operation requires operators to stay in the high-altitude cab. Heavy load, high-altitude and open-air operation scenarios are prone to safety accidents such as falling, collision and box falling. Meanwhile, the risk of severe weather operation is extremely high.

    Lower labor costs

    RTG operation of traditional container terminals requires a large number of certified operators, on-site management personnel, inspection personnel, labor compensation, skill training, post management, safety guarantee and other labor costs remain high, and the shortage of professional operators in the industry is large, personnel mobility is high, and manpower control is extremely difficult.

    Henan Mine Crane manufactured automatic RTG does not need on-site operators, only a small number of operation and maintenance personnel and central control dispatching personnel can complete the management and control of multiple equipment, which can reduce more than 70% of the front-line operation manpower configuration and greatly reduce the comprehensive labor costs such as labor compensation, training, management and social security.At the same time, intelligent operation and maintenance of equipment can reduce manual inspection costs, reduce economic losses caused by human operation errors, and achieve significant cost reduction benefits for long-term operation.

    Better management

    Relying on digital and intelligent management and control system, automatic RTG completely changes the extensive and empirical management mode of traditional terminals and realizes refined, standardized and digital global management.All operation processes, operation data, energy consumption data and fault records of equipment can be automatically saved and uploaded in real time to form complete data accounts, supporting operation traceability, data statistics and report generation.

    Management personnel can monitor the operation status, equipment operation conditions and operation progress of the yard in real time through the cloud platform, accurately grasp the port operation data, and realize global control without on-site inspection.At the same time, the intelligent dispatching system can independently optimize the operation process, reasonably allocate operation tasks, avoid resource waste and operation conflict, greatly improve the overall operation management efficiency and standardization level of the port, and assist the port to realize digital transformation and upgrading.

    Energy savings

    Traditional manual RTG operation energy consumption control is extensive, operators start and stop at will, high-speed operation, invalid idling and other problems are common, equipment energy consumption waste is serious, and operation energy consumption cost remains high.Automatic RTG is equipped with intelligent energy-saving control system, which can dynamically adjust the operating power and operating speed of equipment according to operating conditions, load weight and operating distance, so as to eliminate ineffective energy consumption.

    At the same time, the equipment is equipped with an energy recovery system, which can recover and reuse the excess energy generated in the process of lifting braking and walking deceleration to further reduce energy consumption.The measured data show that the comprehensive energy consumption of automated RTG is 15%-25% lower than that of traditional manual equipment, greatly reducing port energy consumption expenses and reducing carbon emissions, which is in line with the industry development trend of green port and low-carbon logistics.

    Automated RTG Crane Applications in Modern Smart Ports

    Container yards

    Container yard is the core and most extensive application scenario of Henan Mine Crane manufactured automated RTG.Port yard undertakes the core functions of container stacking, sorting, sorting and transit. Traditional manual operation has low efficiency, chaotic stacking and low site utilization.With the advantages of flexible walking, accurate stacking, intelligent sorting and 24-hour operation, automatic RTG can independently complete the classified stacking, regular placement and batch sorting of import boxes, export boxes and transfer boxes.Through intelligent algorithm optimization of storage scheme, standardized storage of containers in zones, classifications and layers is realized, space utilization rate of storage yard is maximized, idle space and waste of storage yard are reduced, convenient and efficient container access is ensured, turnover efficiency of storage yard is greatly improved, and large-scale container storage and transit demand of large ports are met.

    Port terminals

    In modern seaports and river port container terminals, automatic RTG is the core hub equipment connecting quayside crane and horizontal transportation equipment, undertaking the key tasks of container loading, unloading, transshipment and stacking.The equipment can cooperate seamlessly with quayside bridge, AGV unmanned transport vehicle and truck collection to build a fully automated operation link.Compared with the traditional manual operation mode, automatic cluster operation can completely solve the problems of poor connection, slow turnover and frequent congestion of terminal operation, greatly improve the container throughput capacity of the terminal, meet the operation requirements of rapid loading and unloading and efficient turnover of large ocean-going ships, and is the core standard equipment for upgrading and transforming modern intelligent container terminals.

    Logistics hubs

    The container transit, storage and distribution operation scenarios of inland logistics hubs, comprehensive freight centers and cross-border logistics parks have extremely high requirements on equipment flexibility, operation efficiency and adaptability.With the advantages of trackless flexible walking, strong site adaptability and high degree of automation, automatic RTG can meet the needs of inland hardened sites and multi-area circulation operations.The equipment can complete the whole process operations such as container distribution, temporary storage, sorting and allocation, loading and unloading and transshipment, assist the six logistics hubs to realize standardized, efficient and intelligent control of container operations, break through the barriers of six-sea logistics connection, improve the transfer efficiency of six logistics, and assist the intelligent upgrading of regional logistics industry.

    Terminal upgrades

    Aiming at the intelligent upgrading and transformation scenarios of traditional old docks and traditional manual RTG operation terminals, the automatic RTG transformation scheme has the advantages of high adaptability and high cost performance.There is no need for large-scale renovation of the site or laying of fixed tracks, and intelligent upgrades can be completed on the basis of the original operating site and original equipment.Whether it is partial intelligent upgrading of small and medium-sized terminals or unmanned transformation of large old terminals, automatic RTG can adapt to different upgrading requirements, help traditional terminals complete intelligent transformation at low cost and fast speed, rapidly improve operation efficiency, safety level and operation level, activate old terminal resources and prolong terminal service life.

    Henan Mine Crane Factory Custom

    With the continuous acceleration of the intelligent, digital and green transformation process of global ports, the operation mode of traditional artificial RTG cranes has been unable to meet the efficient, safe and low-cost operation requirements of modern logistics. With the all-round advantages of high-precision operation, unmanned operation, efficient coordination, low-carbon energy saving and intelligent management and control, automatic RTG cranes have become the core equipment of intelligent container terminals and modern logistics hubs.

    As a professional port automation RTG crane source manufacturer, Henan Mine Crane Factory has been deeply engaged in the R & D and customization of intelligent lifting equipment for many years, adapting to the needs of the whole scene such as upgrading of old and new terminals and transformation of logistics hubs.We provide one-stop services for equipment customization, system integration, on-site installation, commissioning and operation, and support personalized intelligent solution customization.Assist the port to greatly improve efficiency, reduce cost, ensure safety, easily realize unmanned and green intelligent upgrading, and avoid pain points of traditional terminal operation.

    Henan Mine CraneDiscuss your requirements ↗
  • Automated RMG vs Manual RMG Crane Which Improves Efficiency More

    Automated RMG vs Manual RMG Crane Which Improves Efficiency More

    Automated RMG vs Manual RMG Crane Which Improves Efficiency More

    Rail gantry crane is the core equipment for container logistics, operational efficiency directly affects the yard turnover, operating costs and competitiveness. The current container throughput surge, site congestion is prominent, many enterprises are confused, automation and manual rail gantry cranes which can improve efficiency, we will combine industry data and hands-on experience from multiple dimensions to disassemble, to help enterprises choose the appropriate equipment.

    Why RMG Efficiency Matters in Modern Container Yards

    Accelerated integration of global trade and cross-border logistics upgrading, promoting container throughput year by year, especially coastal hub ports, inland waterless ports, often faced with intensive storage of goods, vehicle congestion, turnover lag and other pain points. According to industry statistics, every 10% improvement in the operational efficiency of the container yard, the overall logistics costs can be reduced by 8%, and RMG cranes, as the core equipment for container storage, loading and unloading, transshipment, directly control the core efficiency of yard operations.

    In ports and intermodal hubs, RMG cranes have become the core equipment for vertical container storage and horizontal transshipment by virtue of the stability of rail travel and the advantages of large-span operation, assuming the role of a key hub connecting the quay bridge, collector trucks and railroad wagons, and its operational efficiency directly affects the smoothness of the entire logistics chain.

    With the promotion of industry 4.0 and smart port construction, automation, digitalization, intelligence has become an inevitable trend of industry transformation, more and more ports and logistics enterprises began to layout automation RMG system, trying to crack the efficiency bottleneck through technological upgrading. But at the same time, manual RMG cranes still play an irreplaceable role in many scenarios by virtue of their flexibility and low-cost advantages.

    What Is an RMG Crane?

    Definition and core functions

    Rail Mounted Gantry Crane is a kind of large lifting equipment running along the rail, used for container storage and loading and unloading operations, the core function is to realize the vertical lifting, horizontal movement and precise storage of containers, which can be adapted to the standard containers of various types such as 20 feet, 40 feet, etc., as well as some of the special containers for the operational needs.

    As the core equipment of the container yard, the typical application scenarios of RMG cranes cover. Coastal port container yard, inland anhydrous port, railroad container yard, large-scale logistics hubs, as well as chemical industry, cold chain and other professional container storage sites, is the key hub equipment connecting water, land, rail multimodal transport, directly determines the turnover capacity and operational efficiency of the yard.

    Key components

    An efficient and stable RMG crane supplied by Henan Mine Crane Factory, the configuration of its core components directly affects the operational efficiency and service life, mainly including five core parts, and at the same time, need to realize the seamless connection with the yard management system.

    1. Gantry structure: Welded with high-strength steel, it determines the span, stacking capacity and operational stability of the crane, and is the basic structure of RMG cranes, and the large-span design can realize simultaneous operation of multiple rows of containers and enhance the utilization rate of the site.
    2. Hoisting system: Composed of motor, wire rope, drum, spreader, etc., is the core of vertical lifting and lowering of containers, hoisting speed and load capacity directly determines the time of a single operation, high-quality hoisting system can be realized, “heavy load slow, light load fast” grading speed regulation, taking into account the efficiency and safety.
    3. Trolley and trolley running system: Trolley is responsible for transverse movement along the gantry beam, trolley longitudinal movement along the track, the two running speed and positioning accuracy, directly affecting the efficiency of the container transfer, frequency conversion speed control system can achieve smooth operation and accurate alignment.
    4. Control system: Divided into manual control and automatic control system, is the core control component of RMG crane, responsible for receiving operating instructions, control of all components of the coordinated operation, accurate control of the whole process of lifting, moving, dropping boxes;
    5. Yard management system integration: Whether it is manual or automated RMG, it needs to be docked with the terminal operating system to realize the real-time synchronization of the box information, operating instructions and equipment status, avoiding operational chaos and improving the overall efficiency of coordination.

    Manual RMG Crane Overview

    How manual RMG cranes operate

    Manual RMG cranes rely on manual control by the operator to complete the whole process of operation, and there are two main modes of operation. First, the operator operates directly in the crane cab, through the joystick, buttons to control the lifting, trolley, trolley operation, real-time observation of the container and site conditions, complete positioning, grasping, stacking and other actions. The second is through the remote console operation, the operator on the ground or in the center control room, with the help of the camera real-time monitoring of the operating scene, remote control equipment operation.

    The whole operation process relies entirely on the operator’s skills and experience. From the alignment and lifting height control when grabbing containers, to the path selection during the moving process and the precise positioning when dropping the containers, each link requires manual judgment and operation, and the operator’s proficiency and reaction speed directly determine the operation efficiency and safety.

    Advantages of manual RMG

    As the core equipment of the traditional mode of operation, manual RMG cranes can be used for a long time, the core lies in its strong adaptability, cost-controllable advantages, especially suitable for small and medium-sized scenes.

    • Low initial investment cost: Compared with automated RMG, manual RMG does not need to carry complex sensors, automation control systems and AI scheduling module, equipment procurement, installation costs can be reduced by 30% -50%, the pressure of the initial investment is small, suitable for companies with limited budget.
    • Strong adaptability to complex scenarios: Manual operation is more flexible when dealing with irregular and non-standard operation scenarios. For example, when dealing with oversized, overweight containers, damaged containers, or chaotic box position in the yard, temporary adjustment of the operation plan, the operator can flexibly adjust the operation rhythm according to the actual situation, avoiding the rigid limitations of automated systems.
    • Convenient deployment and quick start: The operation logic of manual RMG is simple, the operator can be on duty after short-term training, the equipment installation and debugging cycle is short, no need for complex system integration and debugging, which is suitable for the rapid deployment of small and medium-sized yards.

    Limitations of manual RMG

    With the increase of container throughput and the improvement of operation standard, the limitations of manual RMG are gradually highlighted and become the core bottleneck to restrict the efficiency improvement.

    • Operator fatigue: Manual operation requires operators to concentrate their attention for a long time, and long-time operation is prone to fatigue and distraction, which leads to operation errors. Such as container alignment deviation, grabbing instability, drop box offset, etc., not only affect the operational efficiency, but also may cause damage to the container, equipment failure and other safety hazards.
    • Unstable efficiency: The efficiency of the operation depends entirely on the skills and state of the operator. Skilled operators can complete 15-20 operation cycles per hour, while novice or fatigue, the efficiency may drop more than 50%, the overall operating efficiency fluctuations, it is difficult to achieve a stable turnover of the yard.
    • High long-term labor cost: Manual RMG needs to implement 24-hour three-shift operation, a single machine needs to be equipped with 3-4 operators, but also need to be equipped with on-site command, hooker to work with, long-term labor costs remain high, and with the shortage of skilled operators, the cost of manpower rises year by year, and has become a heavy burden on long-term business operations.

    Automated RMG Crane Overview

    How automated RMG systems work

    Henan Mine Crane Factory supply automated RMG cranes, the core is through the software, sensors and intelligent algorithms to achieve the whole process of unmanned or semi-automated operation, without direct human operation, the overall operation relies on three core support.

    1. Fully automated control system: Through the PLC, industrial computers and other core equipment, receiving the yard management system’s operating instructions, automatically complete the container positioning, gripping, lifting, moving, dropping and other full-process actions, without human intervention.
    2. Multi-sensor fusion technology: Equipped with GPS, laser positioning, OCR image recognition, infrared sensors and other equipment, real-time collection of container location, equipment operation status, site environment and other data, to achieve centimeter-level accurate positioning, to avoid collision, offset and other problems.
    3. Intelligent system integration: Deep fusion of AI algorithm, big data analysis and TOS system can realize automatic scheduling of operation instructions, automatic identification and tracking of containers, real-time monitoring of equipment status, and even collaborative operation with automatic guided vehicles, shore bridges and other equipments, to form a full-process automated operation link.

    According to the degree of automation, it can be divided into fully automated RMG and semi-automated RMG, which can be flexibly selected by enterprises according to their own needs.

    Key features of automated RMG

    Compared with manual RMG, the core advantage of automated RMG lies in intelligence, efficiency and standardization, and its key features directly serve to improve efficiency and reduce costs.

    • Remote monitoring and control: Managers can monitor the operation status of multiple automated RMGs in real time in the central control room, including operation progress, equipment parameters, fault warning, etc. Without on-site guarding, one monitor can supervise 4-8 pieces of equipment at the same time, which greatly improves management efficiency.
    • Automated container identification and tracking: Through OCR image recognition, RFID technology, automatic identification of container number, size, weight and other information, real-time synchronization to the TOS system, to achieve the whole process of container traceability, to avoid confusion, misdirected shipments and other problems.
    • Collision avoidance and safety system: Equipped with infrared sensors, laser collision avoidance devices, can automatically identify personnel, equipment, obstacles within the operating range, timely trigger stop warning to avoid collision accidents, while equipped with emergency braking, overload protection and other functions, significantly improve operational safety.
    • Operation standardization: Each operation is executed by the system in accordance with the preset process, the action is standardized and precise, avoiding human error, while the system automatically records the operation data, which is convenient for subsequent statistical analysis and optimization.

    Automated RMG vs Manual RMG: Efficiency Comparison

    Efficiency comparison is the core basis for enterprises to choose RMG cranes, we are from the six core dimensions, combined with industry test data, comprehensively dismantle the efficiency differences between the two.

    Operational efficiency

    Automated RMG: It can realize 24-hour uninterrupted continuous operation, no need to rest, no fatigue, stable operating rhythm, not subject to the artificial state, rest and relaxation time limitations. Even at night and on holidays, it can maintain stable operational efficiency, which is especially suitable for the continuous turnover requirements of high throughput scenarios. The system can automatically optimize the operation path, reduce ineffective movement, and further enhance the operation continuity.

    Manual RMG: Operational efficiency is completely dependent on the operator’s work and rest and state, need to follow the three-shift system, the actual effective operating time is only 16-18 hours per day, and the efficiency of the operator will be reduced by 30%-40% after more than 4 hours of continuous operation, and at the same time by the impact of food, rest, emotions and other factors, poor operational continuity, prone to wasteful waiting, redundant movements and other issues.

    Henan Mine Crane manufactured’s automated RMGs provide far greater continuity and stability than manual RMGs, increasing time utilization to more than 95%, compared to 70%-80% for manual RMGs. Automation dramatically improves the consistency of the work cycle and avoids fluctuations in efficiency.

    Productivity

    Productivity is the core indicator of RMG efficiency. Taking the number of cycles per hour as the benchmark, combined with the industry’s actual measurement data, the difference between the two is very obvious.

    Automated RMG: Stable and predictable performance, not affected by human factors, under standard working conditions, 25-35 cycles per hour, some high-end automated RMG can exceed 35 cycles per hour, and the efficiency fluctuation error is no more than 5%, suitable for large-scale, high-frequency operation needs. Its high efficiency comes from the precise path optimization and fatigue-free operation advantages, single box operation time can be shortened to 1.5-2 minutes.

    Manual RMG: The operating efficiency fluctuates greatly and is significantly affected by the operator’s proficiency. Skilled operators can complete 15-20 operation cycles per hour, while novice operators can only complete 10-15 cycles, and in the peak of operation, fatigue, the efficiency will be further reduced, fluctuations in error up to 20%-30%, single box operation time of about 2.5-3 minutes, difficult to meet the needs of high throughput scenarios.

    Safety and risk reduction

    Operational safety has a direct impact on operational efficiency and cost, and the difference in safety between the two mainly stems from the difference between human factors and technical protection.

    Automated RMG: Through multi-sensor fusion, intelligent collision avoidance, automatic warning and other technologies, it minimizes human involvement and avoids safety accidents caused by operator fatigue and misoperation. Such as container fall, equipment collision, personnel injury, etc., the accident rate can be reduced by more than 90%. At the same time, the automation system can real-time monitor the equipment operation status, timely detection of potential failures, early warning, reduce the efficiency interruption due to failures, and at the same time reduce the insurance costs and compliance costs.

    Manual RMG: The safety risk mainly comes from the operator’s human error and fatigue operation, according to industry statistics, the incidence of safety accidents in manual RMG is more than 10 times higher than that of automated RMG, and the common accidents include container alignment deviation, unstable gripping and falling, and collision of equipments, etc., which not only affects the operation efficiency, but also generates additional costs such as cargo damage, casualties, and equipment repairs, and at the same time, it needs to bear higher insurance costs and compliance risks. Insurance costs and compliance risks are also higher.

    Automated RMG can significantly reduce downtime losses and compensation costs caused by safety incidents, and at the same time reduce insurance expenses, indirectly improving the overall operational efficiency. Manual RMG, on the other hand, requires more safety management costs and downtime due to accidents, which can further reduce operational efficiency.

    Accuracy and yard optimization

    The accuracy of RMG’s operation directly affects the utilization of yard space and operational synergy, and the difference between the two is mainly reflected in the positioning accuracy and yard optimization capability.

    Automated RMG: Automated rail gantry cranes are equipped with laser positioning, GPS and other technologies, which can realize centimeter-level accurate positioning, deviation of falling containers is no more than 10cm, stacking height is increased by 1-2 layers, and yard space utilization rate is increased by 20%-30%. The system can automatically optimize the planning of box position, reduce invalid movement, and also correct the operation position in real time to ensure accurate docking.

    Manual RMG: Positioning accuracy relies on operator’s experience, the deviation of falling boxes is usually 30-50cm, in order to avoid collision, the stacking height needs to reserve a certain safety space, and the utilization rate of yard space is lower; at the same time, the box position planning relies on manual judgment, which is prone to problems such as chaotic box position, repeated transfer, etc., and increases the ineffective operation time and affects the overall efficiency.

    Automated RMG can improve the utilization of yard space and operation synergy efficiency through accurate positioning and intelligent box position planning, especially suitable for hub yards with limited space and high container throughput.

    Maintenance and downtime

    The downtime of the equipment directly affects the operational efficiency, and there is a significant difference between the maintenance mode and downtime frequency of the two.

    Automated RMG: Automated rail-mounted gantry cranes adopt predictive maintenance mode, collecting equipment operation data through sensors, combining with AI algorithms to predict potential failures and maintain them in advance, which can reduce downtime by 5-15% and increase labor productivity by 5-20%, with an average annual downtime of no more than 50 hours, and with a high-end configuration of core components and a lower failure rate.

    Manual RMG: Manual rail gantry crane adopts passive maintenance mode, equipment failure only after maintenance, no advance warning, sudden failure is frequent, the average annual downtime of 150-200 hours, and most of them occur at the peak of the operation, affecting the turnover of the yard, and its maintenance relies on manual troubleshooting, maintenance efficiency is low, which will further extend the downtime.

    Henan Mine Crane manufactured’s automated RMGs have 1/3-1/4 the downtime of manual RMGs, and through predictive maintenance, they minimize the loss of efficiency caused by breakdowns and downtime, and ensure the continuity of operations.

    When Manual RMG Still Makes Sense

    Despite the significant efficiency advantages of automated RMG, not all scenarios are suitable for deployment. In the following two types of scenarios, manual RMG can still give full play to its flexible, low-cost advantages, and achieve a balance between efficiency and cost.

    Small or low-volume terminals

    For small container yards, inland small anhydrous ports, and sites with low throughput, manual RMG is a more cost-effective choice.

    1. Low investment threshold: Small yards have limited budgets, and the initial investment in manual RMG is only 50%-70% of that in automated RMG, which significantly reduces the upfront investment pressure and eliminates the need for complex system integration and maintenance costs.
    2. Simple operational requirements: Small yards have a small amount of work, slow tempo, manual RMG efficiency can fully meet the demand, without the need to invest in high cost deployment of automation systems, to avoid the use of large materials.
    3. Flexible operation: The operation plan of small yards is easy to adjust, manual RMG can flexibly switch the operation mode according to the actual demand, to adapt to the demand of small batch and multi-batch operation, without complex system debugging.

    Complex or non-standard handling scenarios

    • Oversized, overweight, damaged container handling: Such as handling special containers over 45 feet, overweight containers, or damaged and deformed containers, operators need to flexibly adjust the gripping method and positioning angle according to the actual situation, which is difficult to be adapted to the rigid operation of automated systems.
    • Irregular operation process: Such as temporarily increasing the operation task, adjusting the box position planning, dealing with unexpected situations, manual operation can quickly respond without modifying the system program, to avoid the automated system process rigidity.
    • Limited site conditions: Some old yards have uneven tracks, narrow sites, or no perfect TOS system, making automated RMG deployment difficult and costly, while manual RMG can be quickly adapted without complex site modifications.

    When Automated RMG Is the Better Choice

    When enterprises face high throughput, high labor costs, intelligent transformation and other needs, the efficiency and long-term cost advantages of automated RMG will be fully highlighted, and the following three types of scenarios are the most suitable for the deployment of automated RMG.

    High-throughput container terminals

    For coastal hub ports, large inland anhydrous ports, and yards with average daily container handling capacity ≥1000TEU, automated RMG is the core choice for improving efficiency.

    1. Demand matching: High throughput yards require 24-hour continuous operation, and the uninterrupted operation capability of automated RMG can fully meet the demand, significantly increase the turnover speed of yards, and avoid problems such as container pile-ups and ship stranding in the harbor. 2.
    2. Efficiency advantage: The number of operations per hour of automated RMG is more than 50% higher than that of manual RMG, which can quickly deal with the surge in container throughput, relieve site congestion and improve customer satisfaction.
    3. Scale effect: High throughput yards usually need to deploy multiple RMG, automation system can realize multiple equipment cooperative operation, intelligent scheduling, and further enhance the overall efficiency, while it is difficult to realize the scale of manual RMG cooperation.

    Smart port development trends

    With the development of Industry 4.0 and digital economy, smart port” has become an inevitable trend of industry transformation, and automated RMG is the core equipment for smart port construction.

    • Demand for digital transformation: Automated RMG can be seamlessly integrated with TOS system, AGV, shore bridge and other equipment to form a whole-process automated operation chain, realize digitalization, visualization and intelligence of yard operation, and help enterprises complete digital transformation.
    • Competitiveness Improvement: In the construction of smart ports, the deployment of automated RMG can improve the competitiveness of enterprises in the industry, attract more customers to cooperate, and at the same time, reduce operating costs to achieve quality and efficiency.

    Labor shortage or high labor cost regions

    Currently, ports and logistics industries are facing a shortage of skilled crane operators, and labor costs are rising year by year, in such regions, the advantages of automated RMG are particularly obvious.

    1. Reduce labor dependence: Automated RMG can greatly reduce the need for operators, only 1-2 supervisors are needed for a single machine, which can effectively solve the problem of labor shortage, and no need to worry about the problems of operator recruitment and training.
    2. Reduce labor cost: The long-term labor cost of automated RMG is only 30%-50% of manual RMG, which can save hundreds of thousands of dollars per year in high labor cost areas.
    3. Enhance operational stability: No need to worry about efficiency interruptions caused by operators leaving or taking leave, the automated system can maintain stable operations and guarantee the continuity of yard turnover.

    Cost vs Efficiency: Which One Wins?

    Enterprises choose RMG cranes, the core is to find a balance between cost and efficiency, we are from the initial, investment in long-term operating costs, the whole life cycle cost of three dimensions, to give a clear conclusion.

    1. CAPEX: Manual RMG wins. The initial investment of manual RMG is only 50%-70% of that of automated RMG, which is suitable for enterprises with limited budget and short-term investment, without the need to bear complex system integration costs.
    2. OPEX: Automated RMG wins. The long-term labor cost and maintenance cost of automated RMG are much lower than manual RMG, and a single unit can save 300,000-600,000 RMB per year. The higher the efficiency and the longer the operation time, the more obvious the cost advantage is, which is especially suitable for enterprises with long-term operation.
    3. TCO: Automated RMG is more advantageous. Although the initial investment of automated RMG is high, the investment can be recovered in 3-5 years, and the subsequent long-term operation cost is extremely low, and the total cost in the whole life cycle (15-20 years) is 30%-50% lower than that of manual RMG. Although the initial investment of manual RMG is low, but the long-term labor cost and failure cost keep accumulating, so the total cost of the whole life cycle is higher.

    Henan Mine Crane Factory Custom

    There is no absolutely more efficient RMG crane, only a more suitable choice. The improvement of efficiency depends not only on the equipment itself, but also on the scale of operation, operational needs, budget level and long-term strategy of the enterprise. For the pursuit of scale, efficiency, digitalization of the enterprise, automation RMG is the inevitable choice. For enterprises pursuing flexibility, low cost and short-term return, manual RMG is more advantageous.

    Henan Mine Crane Factory, as a well-known large-scale crane manufacturer in China, can provide customized RMG crane solutions according to the actual needs of enterprises to achieve a balance between efficiency and cost, and help enterprises crack the efficiency bottleneck of yard operations and achieve high-quality development.

    Henan Mine CraneDiscuss your requirements ↗
  • Automated Overhead Crane: The Key to Smart Warehousing

    Automated Overhead Crane: The Key to Smart Warehousing

    Automated Overhead Crane: The Key to Smart Warehousing

    Over the years, the warehousing industry is quietly changing

    As an old engineer in Henan Mine Crane sales and technical services for more than ten years, I have seen too many warehouses because of low material handling efficiency, high labor costs and headaches.

    The automatic Overhead Crane system is the key equipment to solve these pain points, but also an indispensable part of modern intelligent warehousing and industrial logistics.

    Today I will make the automatic Overhead Crane system clear, from its definition, working principle, to the advantages, application scenarios, and then to the procurement of what to pay attention to, to help you take a detour.
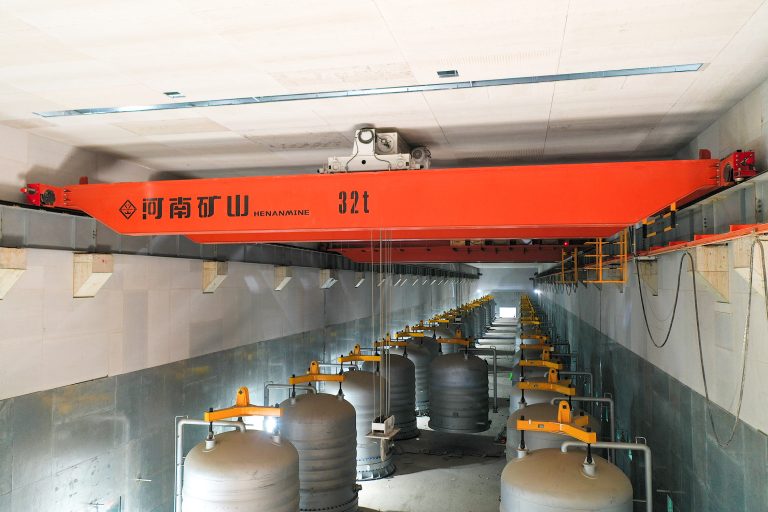
    overhead crane for workshop Henan Mine Crane Factory supply

    What is an automatic Overhead Crane system?

    Basic Definition

    Automatic Overhead Crane System, simply put, is based on the traditional Overhead Crane, integrated with intelligent control, sensors, software and communication technology, without too much human intervention, it can autonomously complete a series of tasks such as lifting, storing and handling of materials.

    It is not like the traditional Crane, must rely on the operator to control the whole process, but through the preset program and real-time monitoring, to achieve unattended or semi-unattended operation, especially suitable for repetitive and regular material handling scenarios.

    Difference with Traditional Overhead Cranes

    Most of the traditional Overhead Cranes are operated manually or semi-manually, the operator has to sit in the cab or control it with remote control on the ground, every action needs manual judgment and operation, which is very dependent on the experience of the operator.

    Automatic Overhead Crane system, on the other hand, relies on the program and the system to make decisions, the operator only needs to monitor in the background and occasionally deal with abnormal situations. The most obvious difference between the two is the difference between “human-controlled” and “self-controlled”.

    Main System Components

    The core components of the automatic Overhead Crane system are actually upgraded on the basis of the traditional Overhead Crane, mainly including these parts:

    The Overhead Crane structure is still the core load-bearing part, which, like the traditional bridge crane, is responsible for supporting the weight of the entire equipment and the loads to be lifted

    Sensors and positioning systems are the “eyes” of automation, such as laser positioning, encoders, limit switches, which can accurately locate the position of materials and Crane, and the error can be controlled in millimeter level

    Warehouse management software (WMS) or central control system is the “command center”, all the actions of the Crane, the
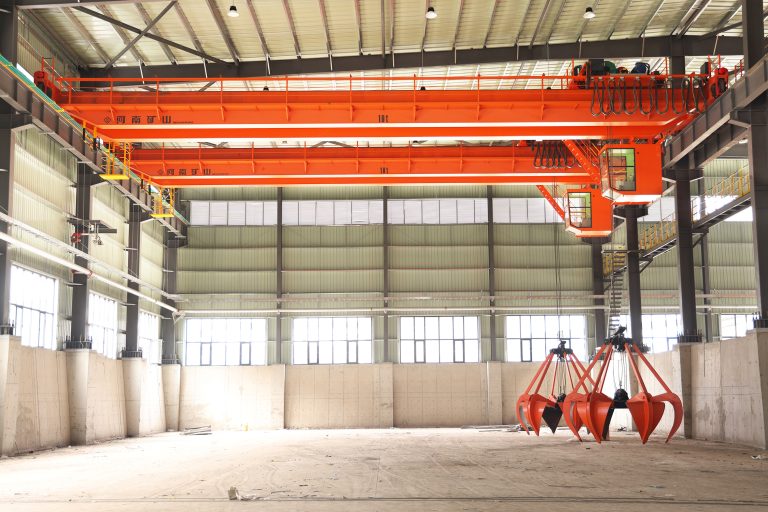
    overhead crane for workshop Henan Mine Crane Factory supply

    Why Smart Warehousing Needs an Automated Overhead Crane System

    The need for faster material flow

    Nowadays, warehouses and production plants have higher and higher efficiency requirements for material handling. Especially in e-commerce warehouses and large logistics centers, thousands of pieces of goods have to be handled every day, and it is difficult to meet the short-cycle and high-frequency handling demand by manual or traditional cranes.

    Automatic Overhead Crane system can realize continuous operation, no need to take a break, and will not be fatigued by the efficiency decline, can effectively shorten the material handling cycle, so that the flow of the entire warehouse speed up.

    Reduce the pressure of labor dependence

    In recent years, labor costs are getting higher and higher, and warehouse handling is repetitive physical labor, young people are not willing to do, resulting in many warehouses are faced with the problem of recruitment difficulties.

    Automation equipment can replace most of the manual operations, such as automatic gripping of materials, transport, storage, do not need manual intervention, both to reduce the number of manual labor, but also reduce the intensity of manual labor, to solve the difficulty of recruiting and retention of the pain point. Many customers feedback, with the use of automated systems, warehouse labor costs can be reduced by more than 30%.

    Demand for higher precision and traceability

    One of the core needs of intelligent warehousing is to accurately manage inventory and reduce handling errors.

    The automatic Overhead Crane system can accurately locate the goods position and materials through sensors and software, and every handling can be recorded in the system, realizing full traceability of materials. This makes inventory management clearer and reduces losses due to errors.

    Demand for safer operations

    Material handling in warehouses, especially for heavy materials, is prone to safety hazards when operated manually.

    Overhead Crane systems can preset safety parameters, such as automatically stopping operations when overloaded, and anti-collision sensors can avoid collisions between equipment and between equipment and warehouse structures, reducing the chances of personnel being exposed to hazardous environments and making operations safer.

    How the Automatic Overhead Crane System Works

    Automatic positioning and operation

    One of the core advantages of the Automatic Overhead Crane system is the precise automatic positioning.

    During operation, after the system sends commands, the Crane automatically recognizes its own position through laser positioning, encoders and other equipment, and then moves along the preset route to the designated pick-up point accurately, the whole process does not require human intervention, and the positioning error can be controlled within 5 mm.

    Load Recognition and Handling

    The system can identify the weight and size of the material through sensors, and can also identify the type and batch of the material through barcode, RFID and other technologies to ensure that the correct material is lifted.

    Integration with warehouse software

    Overhead Crane systems do not operate in isolation, they integrate seamlessly with Warehouse Management Systems (WMS), Manufacturing Execution Systems (MES), Enterprise Resource Planning (ERP) systems and more.

    Data Feedback and Monitoring

    Managers can clearly see the operation of each Crane in the background. In case of malfunction, such as sensor malfunction or motor abnormality, the system will promptly issue an alarm and display the location and cause of the malfunction, which facilitates maintenance personnel to deal with it quickly. At the same time, the data can also provide a basis for subsequent maintenance and optimization, such as the development of a more reasonable maintenance plan based on the frequency of operation.

    Key technologies behind the automatic Overhead Crane system

    PLC and intelligent control systems

    PLC (Programmable Logic Controller) is the “brain” of the automatic Overhead Crane system, which is equivalent to the nerve center of a human being, and is responsible for processing all the commands and logical judgments.

    Sensor and Positioning Technology

    Sensor and positioning technology is the foundation of automated operation, without accurate positioning, there is no reliable automation. Common positioning technologies include laser positioning, encoder positioning, and limit switch positioning.

    Remote monitoring and IoT connectivity

    Most of the automated Overhead Crane systems nowadays support remote monitoring and IoT connectivity. Managers don’t need to be at the warehouse site, just through computers, cell phones and other devices, they can view the Crane’s running status and operation data in real time.

    Anti-Sway and Precise Control

    Automatic Overhead Crane systems are equipped with anti-sway control technology, which can detect the magnitude of material sway in real time through sensors, and then automatically adjust the crane’s operating speed and direction to offset the sway and ensure smooth lifting of materials.

    AI and data-driven optimization

    The application of AI technology in automatic Overhead Crane systems focuses on predictive maintenance, route optimization and job analysis.

    However, it should be noted that the current application of AI in Crane automation is still being gradually improved, do not need to be overly deified, the core is still the basic automation function first, and then gradually upgrade and optimize.

    The main advantages of automatic Overhead Crane systems in intelligent warehousing

    Efficiency Improvement

    Automatic Overhead Crane system can realize 24-hour continuous operation, no need to rest, and will not affect the efficiency because of artificial fatigue and operational errors.

    Moreover, it can realize the cooperative operation of multiple cranes and reasonably allocate tasks to avoid the situation of one busy and one idle, so that the material flow of the whole warehouse is smoother.

    Higher storage and retrieval accuracy

    When manually handling, it is easy to misplace the cargo space and mix up the materials, especially in the warehouse with dense cargo space and many types of materials, the error rate is very high.

    The automated system ensures that each batch of materials can be placed in the correct location through accurate positioning and material identification, and the target materials can be found quickly during retrieval, with an error rate of almost zero. This is very important for warehouses that require accurate inventory management, such as electronic parts warehouses and pharmaceutical warehouses.

    Lower long-term operating costs

    Many customers will initially think that the initial investment of an automatic Overhead Crane system is higher than that of a traditional crane, which is not very cost-effective. But in the long run, it has lower operating costs.

    On the one hand, it can reduce the number of manual labor and lower labor costs; on the other hand, it operates more stably, with a lower frequency of failures than traditional Cranes and lower maintenance costs. And it can reduce the material damage and equipment failure caused by manual operation errors, and indirectly reduce the loss. Generally speaking, the invested cost can be recovered in 1-2 years by the saved labor and loss.

    Safety Improvement

    The automatic system can avoid the safety hazards brought by manual operation, such as overloading, collision and material falling. Its safety protection devices monitor the operation process in real time, and will automatically stop the operation and sound an alarm in case of any abnormality.

    At the same time, the operator does not need to work in the dangerous area, which reduces the risk of personnel injury. Especially in hazardous environments such as high temperature, corrosion, explosion-proof, etc., the advantages of the automatic system are more obvious and can maximize the protection of personnel safety.

    Better data visibility

    The automatic system will collect all the operation data in real time, such as the number of lifting times, load weight, running time, fault records, etc. These data will be uniformly stored in the system, so that the managers can view and analyze them at any time.

    Through these data, you can clearly understand the use of cranes, the efficiency of the material flow in the warehouse, and also find bottlenecks in the operation, such as a certain lifting route is congested, and the load of a certain crane is too high, and then optimize it in a targeted way, so that the warehouse management is more scientific.

    More stable operation

    Manual operation will be affected by emotions, fatigue, experience and other factors, inconsistent movements, which can easily lead to unstable operation of the Crane, such as shaking, running away.

    All the actions of the automatic system are executed in accordance with the preset procedures, with a high degree of standardization, there will be no human error, and the operation is more stable. This reduces the wear and tear of the equipment, extends the service life of the Crane, and also avoids material damage caused by unstable operation.
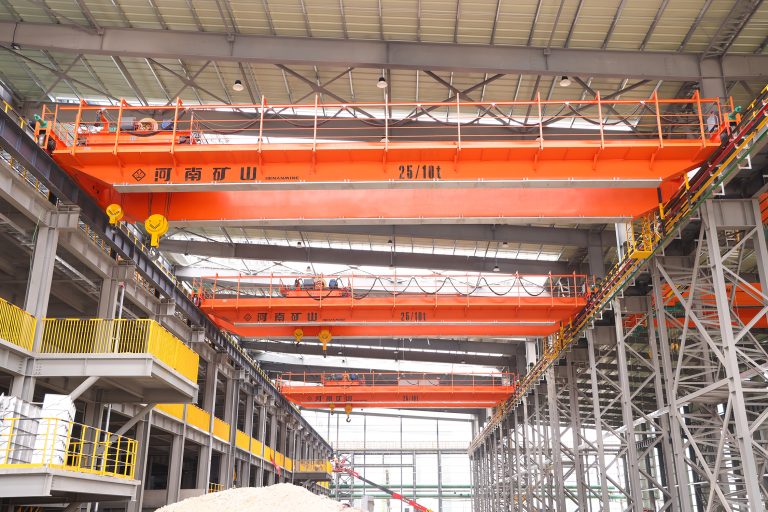
    overhead crane for workshop Henan Mine Crane Factory supply

    Common Applications of Automatic Overhead Crane Systems

    Intelligent Warehouse

    Intelligent warehouses are the most important application scenario for Overhead Crane systems, especially high density storage warehouses. These warehouses are densely populated, and manual handling is difficult and inefficient. The automatic system can make full use of the overhead space to realize automatic storage, retrieval and handling of materials.

    For example, e-commerce logistics warehouses, cold chain warehouses, electronic parts warehouses, every day to deal with a large number of materials, automatic Overhead Crane system can be and AGV, conveyor and other equipment with the formation of a complete automated material flow line, significantly improve the operational efficiency of the warehouse.

    Steel and Metal Handling

    Steel mills and metal processing plants often need to lift heavy materials such as billets, steel plates, profiles, coils, etc. These materials are heavy and frequently handled, with harsh operating environments and high risk of manual operation.

    Automatic Overhead Crane system can adapt to this heavy-duty, high-frequency operation needs, accurate lifting of various types of metal materials, but also with the production line, to realize the automatic feeding of materials, reduce manual intervention and improve production efficiency.

    Manufacturing workshop

    In machinery manufacturing, automobile parts manufacturing and other workshops, the production line requires a large amount of material supply, such as raw materials, parts, finished products and so on. Automatic Overhead Crane system can realize the automatic lifting and conveying of materials, transporting raw materials to the production line, and then transporting finished products to the warehouse, forming the automated closed loop of “Production – Handling – Storage”.

    This not only reduces labor costs, but also avoids production line stoppages caused by untimely material supply and ensures a stable production rhythm.

    Paper Mill and Roll Handling

    Paper rolls in paper mills are heavy, bulky and easily damaged, making manual handling difficult and risky. The automatic Overhead Crane system accurately grabs the paper rolls, lifts and stores them smoothly, and avoids collision and damage to the paper rolls.

    Precast concrete and heavy materials

    Precast concrete plants and building materials plants need to lift heavy materials such as molds and finished concrete components, which are repetitive, labor-intensive and inefficient to handle manually.

    The Automatic Overhead Crane system can adapt to the lifting needs of heavy materials, realize the automatic handling and storage of molds and finished products, reduce manual intervention, lower labor intensity, and at the same time improve the handling accuracy to avoid material damage.

    Dangerous or high temperature environment

    In hazardous or high-temperature environments such as chemical workshops, metallurgical workshops, etc., the risk of manual operation is high, and even normal operation is impossible. Automatic Overhead Crane system can realize unattended operation in these environments to avoid personnel exposure to danger.

    For example, flammable and explosive materials in chemical workshop and high temperature steel ladle in metallurgical workshop can be lifted by automatic system, which not only ensures the safety of operation, but also does not affect the production progress.

    Automatic Overhead Crane System vs Traditional Overhead Crane

    Operation Mode

    Traditional Overhead Crane is mainly operated manually or semi-manually, the operator needs to control every movement of the crane, relying on the experience and skills of the operator, the operation process is flexible, but the consistency is poor.

    Automatic Overhead Crane system is based on program control, the operator only needs to monitor in the background and occasionally deal with abnormal situations, the operation process is standardized and automated, with strong consistency, and does not need to rely on the experience of the operator.

    Labor Requirements

    Traditional Overhead Cranes need to be equipped with specialized operators, a crane needs at least 1-2 operators, high labor costs, and subject to the difficulty of recruiting and the impact of personnel turnover.

    The automatic Overhead Crane system does not require a dedicated operator for the whole operation, only 1-2 managers are needed, responsible for background monitoring and equipment maintenance, which can significantly reduce the number of labor, lower labor costs, and also avoid the impact of personnel turnover.

    Efficiency and consistency

    The efficiency of traditional Crane is greatly affected by the operator’s experience and fatigue, for example, the efficiency of skilled operators is high, while the efficiency of novices is low, and is prone to operational errors, resulting in poor operational consistency.

    Overhead Crane systems have stable efficiency, can achieve 24-hour continuous operation, and all actions are executed in accordance with the preset program, operational consistency is strong, and there will be no human error caused by fluctuations in efficiency.

    Data and system visibility

    The operation data of traditional Crane is difficult to collect and trace, such as the number of lifting, load weight, fault conditions, etc., all need to be recorded manually, which is not only cumbersome, but also prone to errors, and it is difficult for managers to understand the operation status of the equipment in real time.

    The automatic Overhead Crane system can collect all the operation data in real time and feed back to the backstage monitoring panel, so that the managers can check the status of the equipment and the operation data at any time, and also analyze the problems in the operation through the data traceability, which can provide the basis for the management and optimization.

    Initial investment and long-term return

    The initial investment of traditional Overhead Crane is low, which is suitable for customers with limited budget and low operation frequency, but the long-term operation cost is high, which needs to bear high labor cost and maintenance cost.

    Automatic Overhead Crane systems have a higher initial investment, 30%-50% higher than traditional cranes, but have low long-term operating costs and can achieve long-term savings through reduced labor and lower failure losses. long-term returns are more obvious for warehouses with high operating frequency and large scale.

    Is the Overhead Crane system suitable for all warehouses?

    The most suitable conditions

    Automatic Overhead Crane system is not omnipotent, it is the most suitable for these scenarios: high frequency of operation, a large number of repetitive material handling every day; material flow rules, such as fixed pickup point, cargo position, fixed lifting route; high requirements for handling accuracy, the need for accurate inventory management and material traceability; digital warehouse management needs, want to realize the warehouse of intelligence, automation; warehouse scale, low handling efficiency and high cost. handling efficiency is low and high cost.

    Traditional Crane is still sufficient for the situation

    If the operation frequency of the warehouse is low, and only occasional lifting of materials is required every day, such as small spare parts warehouses and small processing plants, traditional Cranes are sufficient.

    There are also warehouses with complex operating processes, many types of materials, different specifications, lifting routes are not fixed, the automation system is difficult to adapt, in this case, the flexibility of the traditional Crane is more advantageous. In addition, the budget is limited, can not afford the initial investment of the automated system customers, choose the traditional Crane more cost-effective.

    Semi-automation as an intermediate option

    If customers want to enjoy the advantages of automation, but do not want to bear the high initial investment, or the workflow has a certain degree of flexibility, semi-automated solutions are a good choice.

    Semi-automated systems do not need to be completely unmanned, but on the basis of the traditional Crane, adding positioning assistance, anti-sway, remote control and other functions, such as the operator can remotely control the Crane on the ground, the system assists in accurate positioning, which not only reduces the intensity of manual labor, but also reduces the cost of inputs, and retains a certain degree of flexibility of operation.

    This solution is suitable for those warehouses that want to gradually transition to full automation, or where there are certain changes in the operating process.
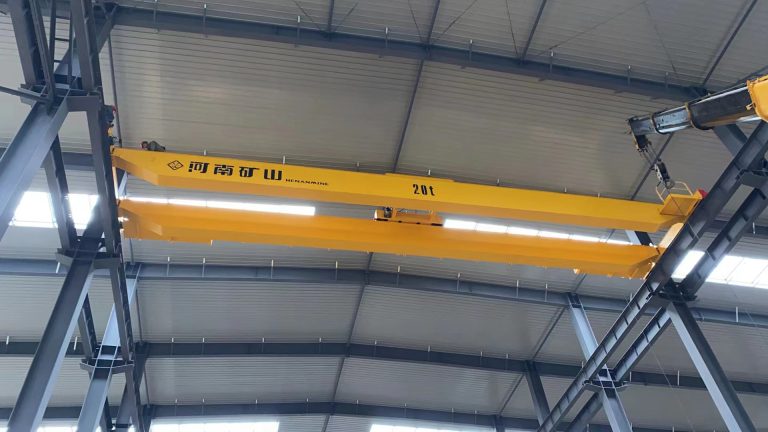
    Double Girder Overhead Crane Henan Mine Crane Mine Factory supply

    Key Factors to Consider Before Choosing an Automated Overhead Crane System

    Material types and handling processes

    First of all, it is necessary to clarify the type of material to be lifted in the warehouse, such as the weight, size and shape of the material, whether it is heavy or light, solid or liquid, and whether it is easily damaged. Different materials have different requirements for the lifting capacity and gripping method of the Crane.

    Warehouse layout

    Warehouse layout is an important basis for the selection of automated systems, you need to provide the warehouse span, Crane running length, lifting height, storage layout, channel width and other data.

    Work level and cycle requirements

    The working level of the Crane determines the durability and stability of the system. Different operating frequency, need to choose a different working level of the system.

    Integration requirements

    The automatic Overhead Crane system needs to be integrated with the existing systems and equipment in the warehouse to maximize the effect. Before choosing, it is important to clarify whether the system needs to interface with software such as WMS, MES, ERP, etc., and whether it needs to work with equipment such as AGVs, conveyors and stacker cranes.

    Safety requirements

    Safety is a prerequisite for automated operations, and different warehouses have different safety requirements. It is necessary to clarify the safety standards of the warehouse, such as whether it needs anti-collision, overload protection, emergency stop, explosion-proof, dust-proof and other functions.

    Maintenance and technical support

    The maintenance of the automatic Overhead Crane system is more complex than traditional cranes, which not only needs to maintain the mechanical components, but also needs to maintain the electrical system and software system. When choosing a supplier, it is important to consider the supplier’s maintenance capability and technical support level.

    Budget and return on investment expectations

    Budget is the main concern of many customers, when choosing an automated system, it is necessary to balance the initial investment and long-term return. You can’t just look at the initial cost, but also consider the long-term operating costs, labor costs, and failure losses.

    Important Features of an Intelligent Automated Overhead Crane System

    Automatic storage and retrieval capability

    This is the most core function of the automatic Overhead Crane system, which can automatically grab materials and transport them to the designated cargo position for storage according to the system instruction, and also can automatically find the target materials and transport them to the designated position according to the retrieval demand.

    This function can realize unmanned handling and storage of materials, reduce manual intervention and improve operational efficiency, especially suitable for high density storage warehouses.

    Accurate Load Positioning

    Accurate positioning is the basis of automated operations, the system can be laser positioning, encoders and other technologies to achieve accurate positioning of the Crane, materials, positioning error control in millimeters.

    Whether storing or retrieving materials, the system can accurately place and grab them, avoiding misplacing and omitting, improving the accuracy of inventory management and reducing material damage.

    Real-time fault diagnosis

    The system can monitor the operating status of the Crane in real time and collect the operating data of the motor, sensors, electrical system and other components. In the event of a fault, such as sensor failure, motor abnormality, or wiring failure, the system will issue an alarm in time and display the location of the fault, the cause, and the treatment recommendations.

    This helps maintenance personnel to quickly locate the fault and handle it in time, reducing downtime and ensuring stable system operation.

    Remote Monitoring Panel

    Managers can view the Crane’s operation status, operation data, fault records, etc. in real time through the remote monitoring panel, which enables comprehensive monitoring of the equipment without the need to be at the warehouse site.

    Predictive maintenance function

    By analyzing the operation data collected by the system, the system can predict the wear and tear of the components in advance, such as the wear and tear of the wire rope, the running status of the bearings, and the aging of the motor, and then send out a maintenance reminder so that the maintenance personnel can carry out maintenance and replace the components in advance.

    Energy-saving operation logic

    The automatic Overhead Crane system is equipped with energy-saving operation functions, such as automatically adjusting the running power of the motor according to the size of the load; automatically reducing the running speed to minimize the energy consumption during no-load operation; and automatically entering into the dormant state to reduce the standby energy consumption when it is not in operation.

    System Expandability

    With the expansion of the warehouse scale and changes in business requirements, the automatic system needs to be scalable, able to upgrade the configuration and increase functionality according to subsequent needs.
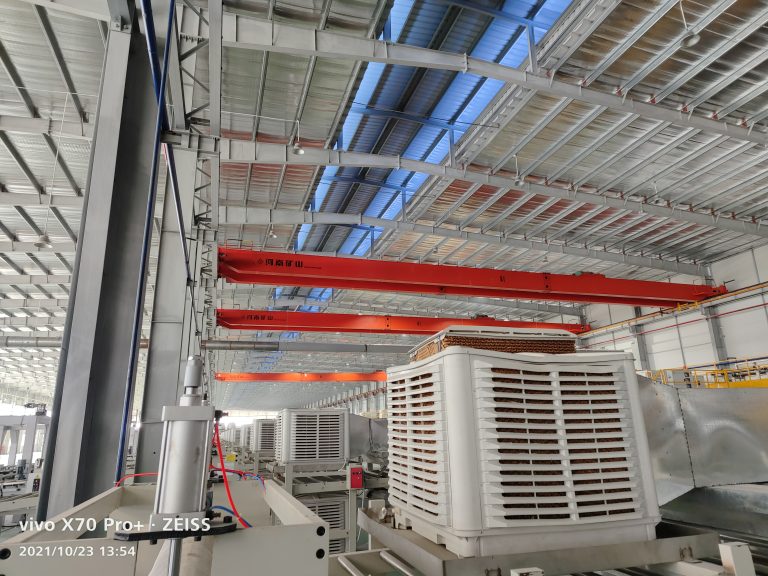
    Double Girder Overhead Crane Henan Mine Crane Mine Factory supply

    Challenges of Implementing an Automated Overhead Crane System

    Higher initial investment

    The initial investment of the automatic Overhead Crane system is quite higher than that of traditional cranes, mainly including equipment costs, installation costs, software integration costs, etc. For SMEs, they may face certain financial pressure.

    Integration complexity

    The automated system needs to be integrated with existing software such as WMS and MES in the warehouse, as well as equipment such as AGVs and conveyors, which is a complicated process and requires a professional technical team for planning and debugging.

    Accurate site data and process planning

    The installation and debugging of automated systems requires accurate warehouse site data, such as warehouse span, lifting height, cargo coordinates, track position, etc. If the data is inaccurate, it will lead to system positioning deviation and poor operation.

    Personnel training and change management

    After the automatic system is put into use, the operation mode of the warehouse will change, and the operators and managers need to adapt to the new way of working, such as learning the skills of backstage monitoring, system operation, and troubleshooting.

    Many old employees are used to the traditional manual operation, and may be resistant to the automation system. It is necessary to do a good job of personnel training and change management, so that employees can understand the advantages of automated systems, master the operating skills and adapt to the new mode of operation.

    Software and control system compatibility

    The software and control system of the automated system needs to be compatible with the existing software and equipment in the warehouse, if the compatibility is not good, it will lead to the system can not run properly

    Therefore, when selecting the system, to ensure the compatibility of the software and control system, it is best to choose a supplier that can provide customized integration services, according to the warehouse’s existing equipment and software, targeted debugging.

    Ongoing maintenance of mechanical and digital systems

    Automatic Overhead Crane systems, with both mechanical components and digital components such as electrical and software, are more complex to maintain than traditional cranes. Mechanical components need to be regularly lubricated, inspected and replaced, and digital components need to be regularly upgraded and debugged to ensure stable operation of the system.

    How Automated Overhead Crane Systems Support Smart Warehouse Strategies

    Better inventory flow management

    One of the core requirements of an intelligent warehouse is to realize accurate management and efficient flow of inventory. Overhead Crane system can be seamlessly integrated with WMS system to update inventory data in real time and realize full traceability of materials.

    Higher Space Utilization

    Overhead Crane system can make full use of warehouse overhead space to realize high-density storage, which can utilize more than 30% more space than traditional manual handling.

    More reliable scheduling and throughput

    The automatic system can realize the cooperative operation of multiple cranes, and reasonably allocate the work of each Crane according to the number of operation tasks to avoid idling or congestion. At the same time, the system can optimize lifting routes, reduce idle time and improve operational efficiency.

    Enhance warehouse digitization level

    Automatic Overhead Crane system can collect real-time operation data, which can provide the basis for the digital management of the warehouse. By analyzing this data, managers can identify bottlenecks in the operation, optimize the operation process, and improve the operational efficiency of the warehouse.

    Laying the foundation for Industry 4.0 development

    The core of Industry 4.0 is intelligence, automation and digitization, and the automatic Overhead Crane system, as the core equipment of intelligent warehousing, can realize the automation and digitization of material handling, and lay the foundation for the transformation of Industry 4.0 for enterprises.

    It can be seamlessly integrated with the production system and management system to realize the whole process automation of “production – handling – storage”, improve the overall operational efficiency of the enterprise and enhance its competitiveness.

    Common Misconceptions to be Avoided on the Purchasing Side

    Focus only on equipment cost

    When purchasing, many customers only focus on the initial cost of the equipment and choose whichever they think is cheaper, while ignoring the subsequent costs of software integration, maintenance, and spare parts.

    Some of the initial cost of equipment is low, but the software integration is difficult, high maintenance costs, the supply of spare parts is not timely, in the long run, the operating costs are higher. Therefore, the procurement should consider the initial cost and long-term operating costs, not just look at the price.

    Neglecting Software Integration Requirements

    The core advantage of the automated Overhead Crane system lies in the integration with warehouse software and other equipment. If the integration needs are ignored and the selected system is not compatible with the existing software and equipment, the advantages of automation cannot be realized.

    Select automation without analyzing the workflow

    For example, the warehouse material handling process is complex, the route is not fixed, the automation system is difficult to adapt, in this case, the choice of traditional Crane or semi-automated system, but more cost-effective. Therefore, before purchasing, you should analyze your workflow and determine whether automation is suitable before choosing the right system.

    Underestimating maintenance and support needs

    The maintenance of automated systems is more complex than traditional Crane, requiring a professional maintenance team and timely technical support, but many customers underestimate the maintenance and support needs when purchasing, and choose a supplier without a perfect maintenance system.

    Excessive automation of simple operations

    Some customers feel that the higher the degree of automation, the better, even if it is a simple operation, but also forced to choose a fully automated system, resulting in over-investment and low cost-effective.

    Not planning for future expansion

    Many customers in the procurement, only consider the current needs, not planning for future expansion, the results of the warehouse scale, business needs increase, the existing system can not be adapted, only to re-purchase equipment, increasing costs.

    Therefore, when purchasing, it is necessary to choose a system with scalability to ensure that the subsequent warehouse expansion, business upgrades, the system can be upgraded by upgrading the configuration, increase the functionality, to meet the new needs, to avoid repeated investment.

    What information should be provided to the automated crane suppliers

    Basic Crane Requirements

    First of all, it is necessary to clarify the basic Crane parameters, such as rated lifting capacity, span, lifting height, running length, operating frequency, which are the basis for the supplier to design the program and select the equipment.

    Warehouse and layout details

    Need to provide the supplier with the architectural drawings of the warehouse, storage layout, distribution of cargo space, aisle width, track location and other details, it is best to provide on-site photos, so that the supplier is clear about the actual situation of the warehouse.

    Material handling process

    It is necessary to explain to the supplier the types, weights, sizes and shapes of materials to be lifted in the warehouse, as well as the material handling process, such as the location of pick-up points and cargo spaces, the planning of lifting routes, the number of lifts per day, and the sources and destinations of materials.

    Automation expectations

    Be clear about your automation expectations, such as whether to choose full automation or semi-automation, whether you need remote monitoring, troubleshooting, predictive maintenance, etc., whether you need to integrate with software such as WMS, MES, etc., and whether you need to work with equipment such as AGVs and conveyors.

    Case: Automatic Overhead Crane in Intelligent Warehouse

    A large e-commerce logistics warehouse: the biggest problem is the high labor cost, requiring 8-10 operators, and low operational efficiency, the number of lifting times per day can not meet the demand, but also often appear misplaced, material confusion, inventory error rate of up to 5% or more, affecting the delivery of orders.

    Later, the customer contacted Henan Mine Crane, according to the actual situation of the warehouse, we designed a set of automatic Overhead Crane system program, equipped with 3 sets of 10 tons of double girder automatic Overhead Crane, docking the warehouse’s existing WMS system, to achieve automatic storage, retrieval and handling of materials.

    After the system was put into use, the number of laborers in the warehouse was reduced to 2 managers responsible for background monitoring and equipment maintenance, reducing labor costs by more than 70%; the number of lifts per day was increased to 1,200-1,500, increasing efficiency by 50%; the positioning accuracy was controlled to within 3 mm, and the error rate of the inventory was reduced to less than 0.5%, significantly improving the efficiency of order delivery.

    At the same time, the system’s real-time monitoring and predictive maintenance features reduce the frequency of failures, downtime has been reduced by 80%, and maintenance costs are 30% lower than traditional Crane. Customer feedback, after this system is put into use, the operational efficiency of the warehouse has been greatly improved, and the invested cost is fully recovered in 1.5 years.
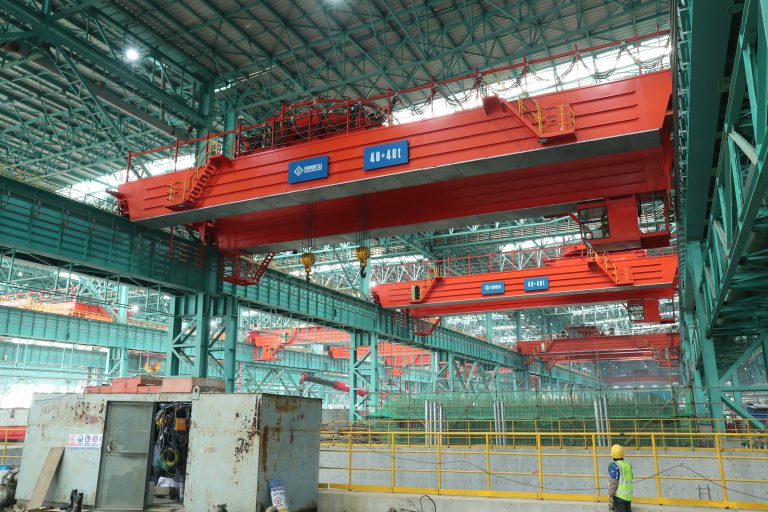
    Upper Rotating Magnetic Electromagnetic Overhead Crane Henan Mine Crane Factory supply

    Frequently Asked Questions about Automatic Overhead Crane Systems

    What is the difference between an Overhead Crane and a Standard Overhead Crane?

    The core difference is the mode of operation and control: standard Overhead Cranes are mainly operated manually, relying on operator’s experience, and the data cannot be traced in real time; automatic Overhead Cranes are mainly controlled by program, realizing unattended or semi-unattended, with real-time monitoring and tracing of data, and higher efficiency and consistency.

    Can Overhead Crane interface with Warehouse Management System (WMS)?

    Yes, and this is one of the core strengths of the Overhead Crane system. It can be seamlessly integrated with WMS, MES, ERP and other warehouse management software to realize the closed loop of order issuance and data feedback.

    Is Overhead Crane only suitable for large warehouses?

    No, it is not only suitable for large warehouses, but also for small and medium-sized warehouses, depending on the frequency of operation and demand.

    Is the Overhead Crane system safe?

    Yes, it is. It is equipped with complete safety protection devices, such as anti-collision sensors, overload limiters, emergency stop buttons, limit switches, etc. It monitors the work process in real time and automatically stops the operation and sends out an alarm in the event of an abnormality.

    Is full automation always necessary, or is semi-automation sufficient?

    Not necessarily, full automation is not the only option, it depends on your operational needs and budget.

    What do I need to prepare before installing an automated Overhead Crane system?

    First of all, it is necessary to organize the detailed data of the warehouse, such as the warehouse span, lifting height, running length, cargo space distribution, track position, etc.,.

    Henan Mine Crane Factory Custom

    Automatic Overhead Crane system, which is becoming the core equipment of intelligent warehousing, is not a panacea, nor is it suitable for all warehouses.

    As a sales and technical expert of Henan Mine Crane, I suggest that before purchasing, you must dock with a professional crane supplier, provide detailed information about your needs, and let the Crane supplier design a customized program according to your actual situation.
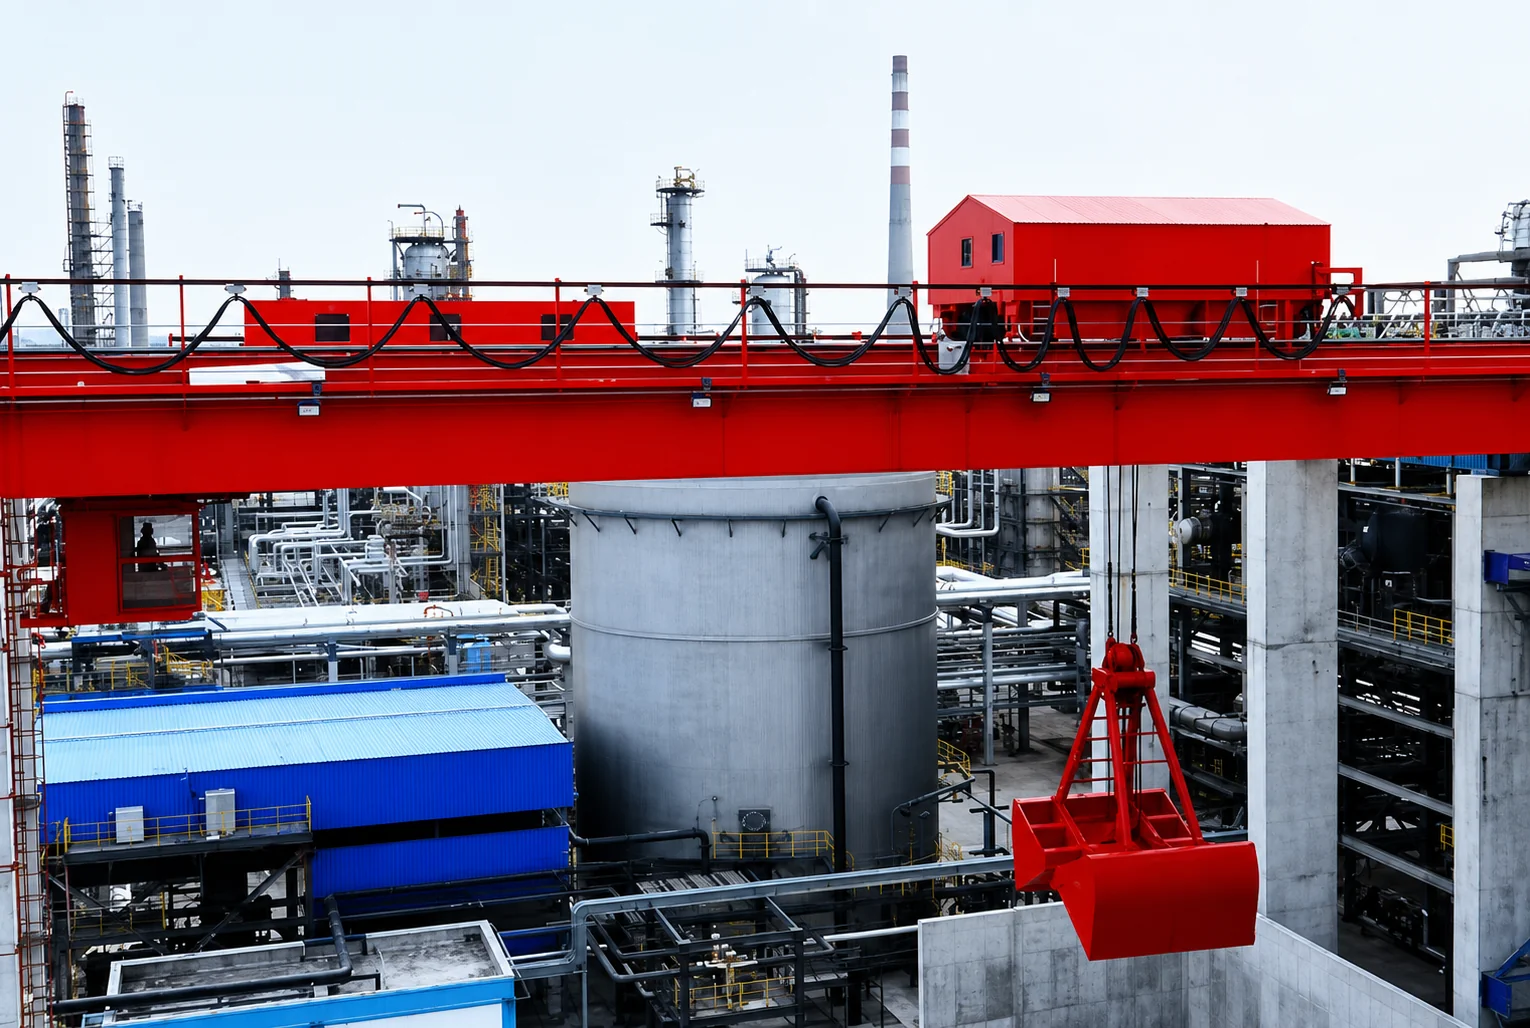
    Henan Mine CraneDiscuss your requirements ↗
  • Automated Intelligent Crane Manufacturer | Custom Solutions & Specifications

    Automated Intelligent Crane Manufacturer | Custom Solutions & Specifications

    Automated Intelligent Crane Manufacturer | Custom Solutions & Specifications

    Decision makers who do industrial material handling can feel the accelerated pace of popularization of automated intelligent crane in recent years. Many purchasing managers, factory engineers, operation and maintenance supervisors looking for intelligent crane selection guide, easy to focus only on the rated tonnage and quotation, ignoring the specification suitability, functional utility and total cost of ownership of intelligent cranes, and finally either the configuration can not keep up with the pace of production, or the input exceeds expectations.

    As a professional intelligent Crane manufactured supplier, Henan Mine Crane Automated Crane Industrial has landed a large number of projects with different working conditions at home and abroad. This content of the intelligent crane specifications selection, core functions, scene adaptation, intelligent crane TCO analysis, operation and maintenance management of the core logic of all speak through, to help material handling decision makers clear from the selection of the whole process to the landing, selected to truly adapt to their own conditions of automated intelligent cranes.


    the basic knowledge of intelligent Crane

    Simply put, the intelligent crane is based on the traditional bridge, gantry lifting equipment, integrated sensor acquisition, automatic control, network communications and data management technology, high-end intelligent lifting equipment, but also the current industrial crane automation upgrade of the core carrier.

    Unlike traditional manual cranes, it can complete standardized material handling through automatic positioning, anti-sway control, path planning and other functions, without the need for operators to manually control the whole process. Highly equipped intelligent unmanned Overhead Crane can realize the whole process of unattended operation, in the high temperature, dust, high-risk operation scenarios, the value is particularly prominent.

    With the advancement of intelligent manufacturing, the technical maturity of this type of equipment is getting higher and higher, from the benchmark demonstration project gradually sinking to the regular reconstruction and expansion projects, suitable for more and more rich working conditions, is no longer the exclusive configuration of the port, large-scale steel mills.

    Overhead Crane Application Cases

     the core technology specifications selection points

    Doing intelligent Crane specifications selection, basic parameter matching is a prerequisite for all intelligent functions to land, away from the working conditions to talk about the configuration is of no practical significance. Each parameter should be combined with on-site operational requirements check, blindly chasing a high or downgraded will affect the subsequent use of the effect.

    The rated lifting capacity covers a wide range, 10-50 tons is common in light and medium-sized workshops, and 100-500 tons can be achieved in heavy-duty metallurgy and port scenarios. Single hook, double hook, special fixture support customization, according to the actual lifting weight to reserve a safety margin, do not get stuck in the rated upper limit selection. For example, steel mill intelligent Crane lifting steel coils, billets, load fluctuations, the margin should be left more adequate.

    The span is customized according to the width of the plant, yard, conventional 10-40 meters, special sites can be made larger span. Intelligent cranes in ports and large logistics parks usually have larger spans to cover a wider operating area. Lifting height determines the stacking and operating range, ordinary workshop 9-15 meters mostly, wharf, high warehouse can be raised as needed.

    The running speed should be selected in combination with the frequency of operation, the general 10-30m/min for empty walking, 20-60m/min for heavy walking, and 5-20m/min for lifting speed, which is not the faster the better, but should be matched with the precision of alignment and safety of operation, and can be increased appropriately for the high-frequency transit scene, and increased for the precision assembly scene. The high-frequency transportation scene can appropriately increase the walking speed, while the precision assembly scene should give priority to ensure the stability of low speed.

    Positioning accuracy is the core indicator of intelligent overhead crane, ordinary configuration can do ±0.1-0.5 meters of fast positioning, high-precision laser plus encoder calibration program, can do ±10mm or even ±3mm, to match the needs of precision assembly, precision stacking. When doing intelligent Crane specification selection, according to the actual alignment needs to choose the accuracy level, do not blindly chase the highest matching.

    The working level should match the intensity of operation, refer to the FEM or CMAA standard selection. High-frequency continuous operation scenarios, such as metallurgical intelligent cranes, three-shift production workshop, can not choose low working level equipment, otherwise it will accelerate the aging of the structure and components, significantly shortening the life of the equipment.

    The mainstream power source is utility-powered electric models, low operating and maintenance costs; outdoor scenes without fixed power supply, you can choose diesel, hybrid or lithium solutions. Environmental adaptation should also be considered in advance, the seaport to do salt spray anticorrosion, dust workshop to do sealed dust, extreme high and low temperature scenarios to do special adaptation, IP protection level, corrosion levels should be clearly written into the technical requirements.

     Core Intelligent Functions

    Sensor monitoring is the basis of all intelligent functions, but also the perception layer of the intelligent Crane safety system. Load sensors monitor the lifting weight in real time, triggering overload protection; position sensors track the real-time coordinates of the trolley, trolley, and hook; wind speed, temperature and humidity sensors collect environmental data, and all the data are summarized to the control system to provide data support for automatic operation.

    At the level of automatic control, intelligent Crane anti-sway control and automatic target positioning are the most commonly used basic functions. Dual closed-loop servo control can control the positioning accuracy at the millimeter level, and the path planning algorithm supports the automatic operation of a single device, as well as multi-machine cooperative operation. Many customers do automation upgrades, the first landing is these two features, the investment is not high but the benefits are obvious.

    Advanced configuration can be added to the algorithmic analysis, machine vision to identify the material and the surrounding environment, algorithms to optimize the scheduling rhythm, assessment of structural fatigue state, to further enhance operational stability. Higher-order projects can also do digital twin, the establishment of a virtual model of the equipment, simulation of the operating process, optimize the scheduling program.

    Intelligent Crane remote monitoring through the Industrial Internet of Things to transmit data to the cloud platform, operating parameters, fault alarms synchronized in real time. Operation and maintenance personnel do not have to go to the scene can initially troubleshoot the problem, software upgrades, log management can be completed remotely, cross-regional, multi-site management scenarios advantages are particularly obvious.

    Intelligent Crane predictive maintenance is a practical and strong cost reduction function, the motor, reducer temperature, current, vibration data collected in real time, the system projects the remaining life of the components, and issue an early warning. Compared with the after-the-fact maintenance that is broken and then repaired, it can significantly reduce unplanned downtime, and is also one of the core functions to pull down the full life cycle cost of intelligent Crane.

    The safety system is multi-level, collision avoidance, electronic limit, emergency stop protection, multi-hook synchronization control, with torque-controlled inverter system, safety redundancy is much higher than traditional equipment. Outdoor models should also be matched with wind speed monitoring and wind protection to further enhance the safety of operations in complex environments.

     the mainstream application scenarios

    Port intelligent cranes are the most mature application of the scene, fully automated shore bridge, dock automation gantry crane can be 24 hours of continuous operation, many large-scale global hub port has completed the scale of intelligent transformation, operational efficiency and labor cost advantages are outstanding.

    Steel mill intelligent cranes, metallurgical intelligent cranes are mainly used for steel coils, billets, iron ladle handling, intelligent transformation can reduce the number of operators on the scene, reduce the risk of high-risk environment operations, with the intelligent Crane predictive maintenance can also reduce the loss of production line downtime.

    Workshop intelligent cranes are suitable for automotive, power equipment, machinery manufacturing and other assembly lines, can accurately distribute materials, reduce manual intervention, suitable for automated production line production beat, enhance the efficiency of the entire production line.

    Warehouse logistics intelligent Crane with three-dimensional warehouse to do unmanned loading, unloading and handling, enhance the efficiency of warehousing turnover, suitable for large logistics parks, e-commerce warehousing, empty container yard and other scenes.

    Energy, mining and other industries also have corresponding specialized models, such as mining intelligent cranes, power plant intelligent lifting equipment, to adapt to heavy-duty, high-risk operational needs, to enhance the safety of field operations.

    Saudi Arabia Port Crane Supplier

     Selection and total cost of ownership (TCO)

    Many customers choose to look only at the purchase price of equipment, in fact, calculate the total cost of ownership of intelligent Crane, to cover procurement, energy consumption, maintenance, downtime losses, residual value and other dimensions, short-term low price is not necessarily cost-effective in the long term. Doing intelligent crane TCO analysis is a necessary part of professional procurement.

    First clear core requirements: maximum lifting weight, lifting height, span, frequency of operation, shift arrangements, matching the level of work according to industry standards, do not lower the configuration in order to lower the budget. Reliable intelligent Crane manufacturing suppliers, will first check the working conditions and then report the program, rather than directly push the standard model.

    Automation level according to the need to choose, not the more full the better. Only need accurate alignment, choose the basic automatic positioning models will be enough; to unmanned operation, and then on a full set of sensing and scheduling system. Initial investment in high program, long-term labor saving, improve efficiency, return cycle depends on the actual amount of work, high-frequency operation of the scene will return much faster.

    Environmental protection can not be saved, poor working conditions, the rate of wear and tear of low-cost equipment will far exceed expectations, later maintenance costs are higher. For example, the coastal harbor intelligent Crane, if the corrosion protection level is not enough, three or five years will appear obvious rust, overhaul cost is very high.

    Energy consumption, electric drive than diesel models have lower operating and maintenance costs. Although the intelligent system increases sensing and software investment, operational efficiency is improved, downtime is reduced, and most projects can recover the incremental cost in a few years. The advantage of customized intelligent Crane solutions is that they can be configured flexibly according to budget and demand, without having to pay for features that can not be used.

    Maintenance costs should also be included in the accounting, sensors, PLC, communication module maintenance costs should be reserved in advance. With intelligent Crane predictive maintenance models, long-term maintenance costs will be lower than traditional equipment, downtime losses are also less.

    Intelligent Crane vs Conventional Crane Core Parameters English Comparison Table


    Item Traditional Crane Automated Intelligent Crane
    Operation Mode Full manual control Auto positioning + semi/unmanned operation
    Positioning Accuracy Depends on operator skill 卤3mm to 卤500mm by configuration
    Safety Level Basic limit & overload protection Multi-layer collision avoidance + predictive protection
    Labor Demand High, depends on skilled operators Lower, one person can supervise multiple units
    Maintenance Mode Breakdown + regular maintenance Predictive maintenance + remote diagnosis
    Data Recording Almost no valid data Full operation & fault data traceable
    Initial Investment Lower Higher by configuration
    Long-term TCO Higher labor & downtime cost Lower for high-frequency operation

     installation and commissioning and operation and maintenance management

    Intelligent Crane installation and commissioning has a clear process requirements, can not be as simple as ordinary overhead crane lifting power on the use. Before installation, the site should be verified, the track, beam bearing and flatness should meet the design requirements, grounding and communication lines laid in place in advance.

    After the equipment is lifted and positioned, the electric control cabinet, frequency converter, all kinds of sensors and operation terminals are installed in turn, and the power supply and network are connected. During the debugging stage of the system, configure the PLC and frequency conversion parameters, verify the intelligent functions such as anti-sway and positioning one by one, and complete the load test and safety performance verification. Before delivery, we give special training to the operators and maintenance personnel, and complete the acceptance after passing the test.

    Daily inspection can not be less, bolt fastening, wire rope wear, electrical interfaces, braking devices, safety devices, every shift to check, there are abnormalities in a timely manner. Preventive maintenance is done according to the cycle, regular replacement of lubricating oil, inspection of brakes, reducers, sensors, cables, according to the manufacturer’s manual.

    Equipment with predictive maintenance function, combined with vibration, temperature, current data to prejudge the life of components, the establishment of maintenance database, more accurate than purely regular maintenance, but also can further pull down the full life cycle cost of intelligent Crane. Control system software should be updated regularly to repair loopholes and supplement functions. Operation logs and maintenance records are archived and retained for subsequent optimization.

    During the life cycle of the whole machine, arrange overhaul according to the plan, and replace the core components in time to the life, which can not only prolong the service time of the whole machine, but also protect the safety of operations.

    Frequently Asked Questions (FAQ)

    Do intelligent Crane selection, the core to see what parameters?

    First check the rated lifting capacity, span, lifting height, working level of these basic parameters, and then according to the operational requirements to determine the positioning accuracy, automation level, environmental protection level, and finally combined with the budget and the total cost of ownership of intelligent cranes to make a comprehensive judgment.

    Can intelligent Crane predictive maintenance really reduce operation and maintenance costs?

    It can. Through real-time monitoring of temperature, vibration, current data of core components such as motors, gearboxes, etc., the aging trend of components can be detected in advance, and scheduled maintenance can be arranged to avoid the loss of production downtime caused by sudden failures, which in the long run can significantly reduce the total operation and maintenance costs.

    What site information is required for a customized smart Crane solution?

    At least to provide site drawings, maximum lifting weight, frequency of operation, environmental conditions, automation needs, existing system interface requirements of this information, engineers can issue accurate customized solutions and quotes.

    How much difference is there between the total cost of ownership of intelligent Crane and traditional equipment?

    Depends on the intensity of operation. High-frequency three-shift operation scenario, intelligent cranes, although the purchase price is high, but manpower savings, downtime reduction, efficiency gains are obvious, a few years will be able to recover the difference in price, the full life-cycle cost but lower; low-frequency operation scenario, you can choose the basic automation configuration, do not have to go on the full set of unmanned features.

    Ordinary old cranes can be upgraded to intelligent cranes?

    Most of the in-service Crane can do intelligent transformation, add sensors, upgrade the electronic control system, increase the anti-sway and positioning functions. Specifically depends on the structure of the equipment, electronic control system adaptability, reliable manufacturers will first do site surveys and then out of the transformation program.

    Conclusion

    Intelligent Crane has been the direction of development of industrial material handling, selection without blindly chasing a high match, combined with their own working conditions, budget and long-term planning, choose to match the configuration is good. Do a good job of intelligent crane specifications selection, calculate the total cost of ownership of intelligent Crane, with standardized operation and maintenance management, the equipment will be able to create a stable value in the full life cycle.

    Why choose our intelligent Crane program?

    Henan Mine Crane is a professional automated crane industrial equipment manufacturers and solution providers, engineering team can be customized according to the customer’s working conditions of the intelligent Crane program, products in line with FEM, CMAA, ISO and other types of industry standards, is a trusted intelligent Crane manufacturers customized service providers.

    Our equipment has passed the relevant quality and safety certification, integrated with IoT and automatic control technology, covering the full range of configurations from basic positioning to fully unmanned operation, and can provide a full set of intelligent functions such as predictive maintenance, remote monitoring and safety protection of intelligent cranes, and support the docking of factory management systems, such as ERP, MES, and WMS.

    From site survey, installation and commissioning to operation training, lifelong technical support, the whole process of follow-up services, there are a number of projects at home and abroad landing experience, can quickly respond to the needs of customers around the world. If you have intelligent Crane procurement, intelligent transformation of old equipment needs, welcome to contact our automation technology team, we will be based on your site conditions, issued by the appropriate selection program.

    Henan Mine CraneDiscuss your requirements ↗
  • Automated Crane Systems: The Future of Smart Industrial Material Handling

    Automated Crane Systems: The Future of Smart Industrial Material Handling

    Automated Crane Systems: The Future of Smart Industrial Material Handling

    With the full implementation of industry 4.0 and intelligent manufacturing, traditional manual control cranes have been unable to adapt to the efficient, safe and accurate operation needs of modern factories, intelligent warehousing, ports, heavy industries and other scenarios.

    The automated crane system integrates a number of intelligent technologies to optimize the traditional handling mode and solve pain points such as inefficient and high-risk operations. It has become the core just-needed equipment for industrial intelligent upgrading and safe cost reduction.

    What Is an Automated Crane System?

    The automated crane system is an intelligent lifting equipment that integrates cutting-edge technologies such as artificial intelligence, machine vision, industrial sensing, automatic control, and the Internet of Things. It can independently complete the whole process of material handling operations such as grabbing, lifting, translation, positioning, and stacking of heavy objects with very little manual intervention or even unattended.

    Compared with traditional lifting equipment, the system has realized a leap from “manual control” to “program automatic control, intelligent decision-making, and data operation and maintenance”, and is adapted to various complex, high-risk, and high-frequency industrial handling scenarios with standardized, high-precision, and high-stability operating capabilities.

    After years of technological iteration, automated cranes have been upgraded from simple electronic control equipment in the early days to an integrated intelligent system that integrates frequency conversion drive, intelligent anti-swing, digital twin, and cloud monitoring. It is deeply connected to enterprise WMS warehouse management, MES production execution, ERP enterprise management and other systems, and has become the core supporting equipment of smart factories.

    Core components

    A complete set of automated crane system is an organic whole of multi-layer technical collaboration. Each component performs its own duties and cooperates in linkage to ensure the stable operation of the equipment. The core composition includes seven modules.:

    • l The main structure and lifting mechanism of the crane: The core mechanical carrier of the equipment, including the bridge, trolley, lifting hoist, operating track and other structures, is responsible for heavy object carrying, lifting and translation operations, and is the hardware basis for automated material transfer.
    • l PLC industrial control system: The “brain” of the intelligent crane, which is responsible for co-ordinating all operating logic, accurately controlling all actions such as lifting, trolley movement, and bridge operation, and executing instructions such as safety interlocking, action timing, and motion trajectory to ensure that the operation process is unified and the error can be controlled.
    • l Sensor and positioning system: The “perceptual nerve” of the equipment, including encoders, laser rangefinder, RFID tags, load cells, proximity sensors, etc., collects data such as equipment location, load weight, operating distance, and surrounding environment in real time to provide accurate data support for intelligent control.
    • l Remote control and HMI human-computer interaction system: abandon the traditional wired handle control mode, equipped with wireless remote control, HMI touch screen, SCADA data kanban board, operators can remotely monitor the status of the equipment, issue operating instructions, and view operating data in real time, making the operation more flexible and intuitive.
    • l Machine vision and AI intelligent technology: relying on high-definition cameras and AI algorithms to achieve load recognition, scene perception, autonomous obstacle avoidance, and balance calibration, it can independently judge the operating environment and optimize the operating trajectory without manual intervention, minimizing manual intervention.
    • l Integrated warehousing/production management system: it can seamlessly interface with industrial systems such as WMS warehousing management, MES production execution, ERP enterprise management, AGV robots, etc. To achieve data exchange and equipment collaboration, so that lifting operations can be integrated into the closed loop of enterprise intelligent production.

    How Automated Crane Systems Work

    Automated load handling

    The automated crane can independently complete the whole process of heavy object grabbing, lifting, translation, positioning, stacking, and palletizing according to preset procedures and production tasks, completely replacing manual repetitive operations.

    Through load cell, RFID scanning, and visual recognition technology, the system automatically detects and identifies the load specifications, weights, and models, and starts the operation process after confirming that the material information is correct, effectively eliminating the problem of manual wrong moving and missing moving.

    In scenarios such as intelligent warehouses and production workshops, the equipment can realize unmanned loading and unloading, transshipment, and stacking operations around the clock, greatly shortening the material handling cycle, and solving the problems of low efficiency and fatigue of traditional manual operations.

    Intelligent positioning and navigation

    In order to solve the pain points of large positioning deviations of traditional cranes and the need for manual and repeated calibration, automated bridge cranes are equipped with multi-dimensional positioning technology, integrating laser ranging, absolute encoder, RFID ground sensing tag, visual camera, inertial measurement unit and other equipment to accurately lock the real-time position of hooks, trolleys, and bridges in real time.

    Relying on LiDAR LIDAR space surveying and mapping, ultrasonic ranging, inertial navigation and other technologies, the equipment can realize autonomous navigation and target position recognition under complex working conditions, and the positioning accuracy under high-end working conditions can reach ±5mm, which fully meets the requirements of high-precision operations such as steel processing, precision manufacturing, and high-end warehousing, without manual secondary correction.

    Intelligent anti-swing and precise control

    When operating traditional wire rope cranes, heavy objects are prone to sway drastically. Not only will it take up nearly one-third of the operating time for stabilizing the hook, reducing operating efficiency, it may also collide with peripheral equipment, damage materials, and even cause safety accidents. It is a key bottleneck restricting the automation upgrade of lifting operations.

    The automated crane is equipped with intelligent anti-swing algorithm and motion control system, which can suppress the swing of heavy objects in real time, reduce the swing amplitude by 85%-95%, and run smoothly and controllably. The positioning accuracy is effectively improved, the operating cycle is shortened, and the safety and efficiency of the operation are guaranteed simultaneously.

    Real-time monitoring and data collection

    Through industrial Internet of Things sensors, automated cranes can collect core data of equipment operation around the clock, rely on the cloud platform to realize real-time visualization of equipment status, and support managers to remotely monitor equipment working conditions and query operation data.

    The system combines big data analysis technology to accurately predict equipment failures and evaluate component life, upgrading traditional passive operation and maintenance to intelligent predictive maintenance.The system can reduce the unplanned downtime of the crane by 28% and increase the service life of the parts by 15%, effectively solving the problems of blind operation and maintenance and sudden failures.

    Key Technologies Behind Smart Crane Automation

    The efficient and safe operation of automated cranes relies on the integration and empowerment of a number of cutting-edge industrial technologies, and the core technology system covers all dimensions of control, interconnection, intelligence, and operation and maintenance.:

    • l PLC automation control technology: As the core control unit of the equipment, it integrates modules such as frequency conversion drive, sensor acquisition, and safety interlocking to accurately execute the operation timing, motion trajectory, and safety protection logic to ensure standardized and zero-error operation of the operation.
    • l Industrial Internet of Things (IIoT) interconnection technology: break the silos of equipment data, realize the data exchange of PLC, drive, sensor, and cloud system through standardized industrial protocols, and support multi-device collaborative operation, remote data transmission, and working condition monitoring.
    • l AI and machine vision technology: realize material recognition, environmental perception, autonomous obstacle avoidance, and load balancing calibration, so that the crane has “vision” and “thinking ability”, adapts to complex and changeable operation scenarios, and improves automation adaptability.
    • l Digital twin and simulation technology: build a virtual image of the equipment, which can simulate the operating status of the equipment, reproduce the historical operating process, test the control program, predict the operating risks, and provide accurate data support for equipment debugging, optimization, and troubleshooting.
    • l Edge computing and cloud platform technology: edge computing realizes real-time processing and instant response of on-site data to avoid security risks caused by network delays; cloud platforms realize data storage, big data analysis, remote operation and maintenance, and equipment cluster management.
    • l Wireless communication technology: relying on the advantages of 5G high-speed, low-latency, and multi-device parallel, it realizes real-time communication between cranes, terminal equipment, sensors, and cloud systems to ensure the stability of remote control, data transmission, and intelligent linkage.
    • l Intelligent safety sensing and obstacle avoidance technology: equipped with radar and laser anti-collision sensors, it can accurately identify surrounding obstacles, personnel, and equipment, and automatically delineate virtual safety operating areas to achieve automatic deceleration and emergency shutdown to prevent collision accidents.

    Key Technologies Behind Smart Crane Automation

    Improve the safety level of operations

    Automated cranes have completely changed the mode of manual near-height hazardous operations, stripping operators from dangerous operating environments such as high temperature, dust, heavy load, high altitude, flammable and explosive, and reducing personal safety risks from the source.At the same time, the equipment comes with multiple safety mechanisms such as collision protection, overload protection, emergency shutdown, and limit protection. It relies on sensors and software systems to realize the whole process of safety control, which can avoid more than 90% of safety accidents caused by human operation errors, and build an intelligent safety operation system.

    Improve production efficiency

    Compared with the randomness and hysteresis of manual operation, automated cranes rely on optimized motion trajectories and standardized operating procedures to operate faster and with shorter cycles. There are no problems such as manual fatigue, shift changes, and errors, and they support 24-hour uninterrupted continuous operation.The measured data show that after the enterprise replaces the intelligent lifting system, the material handling efficiency can be increased by 25%-35%, and the equipment downtime can be greatly reduced, effectively cracking the bottleneck of material transfer in the production line and helping to upgrade production capacity.

    Millimeter-level high-precision operation

    Traditional manual hoisting and positioning errors are large, which can easily cause material bumps and misplaced placement, causing material loss and production delays.Through intelligent algorithms and high-precision sensing and positioning, the automated crane realizes the whole process of automation and precise positioning. The positioning accuracy of high-end working conditions can reach ±5mm, and the operation is consistent and highly repeatable, greatly reducing material damage and operating errors, and ensuring the standardization of production processes. Advance.

    Reduce long-term operating costs

    Automated cranes greatly reduce the dependence on skilled lifting operators, and reduce labor wages, training, and management costs.At the same time, the frequency conversion drive system optimizes energy consumption and reduces power loss; the predictive maintenance mode avoids sudden equipment failures and large maintenance costs, and extends the service life of the equipment.Short-term investment and long-term throttling effectively reduce the overall production operation and equipment operation and maintenance costs of the enterprise.

    Visual control of operational data

    Relying on the Internet of Things and cloud monitoring systems, enterprises can grasp the operating status of equipment, job data, load parameters, and fault information in real time, and realize the visualization, traceability, and analysis of the whole process of the job.Through historical data re-disk and performance data analysis, the operation process can be accurately optimized, equipment resources can be allocated, data support can be provided for production decisions and equipment upgrades, and refined operation and management can be realized.

    Automated Crane Systems vs. Traditional Crane Operation

    In order to more intuitively show the differences between the two, a comprehensive comparison of traditional cranes and automated cranes is carried out from the core operation dimension.:

    Contrast dimension Traditional crane Automated crane
    Operating mode Purely manual control, strong randomness of operation Fully automatic/semi-automatic procedural operation, high degree of standardization
    Security Relying on operator experience, high safety risk Sensor + software dual protection, intelligent anti-collision, overload protection, controllable safety
    Positioning accuracy Manual positioning, large error, need to be corrected repeatedly Millimeter-level high-precision automatic positioning without manual intervention
    Data collection Data is limited, relying on manual records, and data is seriously missing IoT collects full-dimensional operation data in real time, and can be traced throughout the process
    Working time Limited by manual shifts, unable to work continuously for a long time Support 7×24 hours of uninterrupted operation, suitable for high-intensity production
    Operation and maintenance mode Regular manual inspection, passive emergency repair of faults Data-driven predictive maintenance, predict failures in advance, and reduce downtime
    System integration The equipment runs independently and cannot be connected to the intelligent production system Seamless integration with WMS, MES, ERP, AGV and other industrial systems, integrated into the closed loop of intelligent production

    Industrial Applications of Automated Crane Systems

    With the core advantages of safety, high efficiency, precision and unmanned, automated cranes have been widely adapted to complex industrial scenarios in multiple industries, covering warehousing, heavy industry, manufacturing, ports, energy and other fields:

    Intelligent storage warehouse

    The automated crane is deeply integrated with the intelligent warehousing system to realize the unmanned operation of the whole process of automatic warehousing, stacking, retrieval, and outbound of goods. It is perfectly adapted to the intelligent warehouse scenarios of high-level shelves, intensive warehousing, and high-frequency turnover, so as to improve the efficiency of warehousing and circulation and space utilization, and help the intelligent upgrading of warehousing.

    Steel and metal processing industry

    For large-weight materials such as steel coils, billets, sheets, and heavy-duty profiles in steel and aluminum processing scenarios, automated cranes can operate stably under harsh working conditions of high temperature and high dust, and are suitable for continuous casting, rolling, finished product transportation, storage and stacking. It is the core supporting equipment of metal heavy industry production lines.

    Modern manufacturing plant

    In the fields of automobile manufacturing, machining, equipment manufacturing, etc., automated cranes can realize the automatic transfer of materials, parts, and large-scale equipment between the various stations of the production line, accurately connect the production beat, adapt to the punctual production mode, and can work with assembly lines and intelligent robots to open up the closed loop of production material flow.

    Ports and container terminals

    In the scenarios of ports, terminals, and logistics hubs, automated lifting equipment can realize the automatic loading, unloading, transshipment, and storage of containers and bulk cargo, support remote centralized control, greatly improve the throughput efficiency of port cargo, reduce labor investment, and adapt to the high-intensity operation needs of large logistics hubs.

    Foundry and heavy industry

    There are high-temperature, high-dust, high-load, and high-risk operating environments in foundry, mining, heavy industry and other industries. Automated cranes can replace manual completion of high-risk operations such as heavy-duty material transfer and equipment hoisting, reducing personnel safety risks from the source and ensuring the stability and continuity of operations under harsh working conditions.

    Energy and high-risk special environment

    In flammable, explosive, high-radiation, and high-hazard energy scenarios such as power plants, wind power, nuclear power, and chemical industry, special explosion-proof automated cranes can realize unmanned remote operation, meet the safety specifications and operating requirements of special working conditions, and solve the problems of manual operation in high-risk environments.

    What to Consider When Selecting an Automated Crane System

    Automated cranes are customized industrial equipment. The selection needs to be combined with the actual working conditions, production needs, and long-term planning of the enterprise. The core selection points are as follows:

    • l Rated lifting weight and lifting height: select the type according to the maximum load of the material and the operating height to prevent insufficient load from restricting production, while avoiding unnecessary cost waste caused by redundant parameters.
    • l Equipment span and operating distance: combined with the actual size of the workshop, warehouse and other work sites, match the crane span and operating stroke, and adapt to the site layout specifications.
    • l Working level and operating frequency: According to the daily operating time, operating frequency and load rate of the equipment, the corresponding operating condition level is selected. High-frequency and heavy-duty scenarios need to be matched with enhanced mechanical structure and electronic control system.
    • l Positioning accuracy requirements: match accuracy parameters on demand, adapt to ±50mm conventional accuracy for ordinary warehousing, and choose ±5mm high-precision systems for high-end scenarios such as steel processing and precision manufacturing.
    • l Operating environment conditions: distinguish between indoor and outdoor operating scenarios, and select appropriate protection and explosion-proof equipment for special operating conditions such as high and low temperature, dust, humidity, flammable and explosive.
    • l Existing system compatibility: Ensure that the equipment can be seamlessly connected to the enterprise’s existing PLC, WMS, MES, ERP and other management systems to break through data silos and achieve global collaboration.
    • l Safety and emergency configuration: Equipment needs to be equipped with emergency stop, limit, overload protection, intelligent anti-collision and other functions as standard, in line with ISO, FEM, OSHA and other international safety standards.
    • l Remote operation and maintenance capabilities: Priority is given to equipment that supports remote monitoring, fault diagnosis, and online debugging to effectively reduce the difficulty and labor costs of late operation and maintenance.
    • l Extensibility: Equipment reserves space for functional upgrades, capacity expansion, and module expansion, which can be adapted to the subsequent capacity upgrades and process iteration needs of enterprises.

    Challenges of Implementing Crane Automation

    Despite the significant advantages of automated cranes, enterprises still face a number of core challenges in the process of upgrading, which need to be avoided in advance and dealt with scientifically:

    • l The initial investment cost is higher: the automation system includes high-end configurations such as electronic control, sensing, AI, and the Internet of Things. The initial investment in equipment procurement, system commissioning, and site transformation is much higher than that of traditional cranes, and there are certain requirements for the initial capital investment of the enterprise.
    • l It is difficult to be compatible with old equipment: The existing traditional cranes of some enterprises are old equipment, the mechanical structure and electronic control system are old, and the adaptability to the new automation module is poor. There are problems of high difficulty and high cost of transformation.
    • l Insufficient sensor stability under harsh working conditions: high temperature, high dust, strong vibration, and humid industrial environments can easily affect the accuracy and stability of sensors, cameras, and communication equipment. Industrial-grade reinforcement accessories are required.
    • l Network and data security risks: After smart devices are connected to the Internet, there is a risk of network fluctuations, data leakage, and system intrusion. It is necessary to build a dedicated industrial network and improve the network security protection system.
    • l The problem of personnel skill transformation: Automation equipment does not require manual operation, but professionals are required to be responsible for programming, debugging, operation and maintenance, and data analysis. Traditional operator skills cannot be adapted to new equipment, and special skills training is required.
    • l Complex system debugging and operation and maintenance: the automation system integrates mechanical, electrical, software, and algorithm technologies in multiple fields, and the equipment debugging, troubleshooting, and daily operation and maintenance are extremely professional, relying on professional technical teams.
    • l The scarcity of high-quality cooperative manufacturers: crane automation upgrading is not a simple addition of assembly parts, it requires the integration of multiple disciplines and technologies, and the selection of inexperienced manufacturers is prone to problems such as poor system adaptation, unstable operation, and unsecured after-sales service.

    How to Maximize ROI From Crane Automation

    In order to enable enterprises to achieve long-term and efficient returns on their investment in automation equipment, seven strategies can be used to optimize the landing effect and improve the ROI:

    • l Give priority to upgrading high-value and high-risk processes: give priority to the automation and transformation of high-risk operations, high-frequency duplication, and efficiency bottlenecks in the handling process, so as to quickly realize safety upgrades and efficiency improvements, and quickly recover costs.
    • l Formulate quantifiable automation assessment indicators: clarify core KPIs such as operation cycle, positioning accuracy, equipment utilization rate, production capacity improvement rate, and failure rate, accurately measure the effect of automation transformation, and continuously optimize the operating model.
    • l Focus on the core improvement goals of safety and efficiency: relying on the safety protection and efficient operation advantages of automation equipment, give priority to solving safety hazards and production capacity bottlenecks, and consolidate core benefits.
    • l Open up the factory-wide data linkage system: connect crane operation data to the factory-level intelligent management system to realize data sharing and collaborative work, and optimize the overall production scheduling efficiency.
    • l Pre-planning scalable architecture: reserve space for expansion and upgrade during the equipment selection and system construction stages to adapt to the future production capacity expansion and process upgrade needs of the enterprise, and avoid waste of secondary transformation.
    • l Choose modular automation technology: choose modular PLC, sensor, and communication modules to support step-by-step upgrades and partial replacements to reduce the cost of late iterative transformation.
    • l Establish a long-term operation and maintenance guarantee system: formulate a standardized regular operation and maintenance plan, rely on predictive maintenance functions to check for faults in advance, reduce unplanned downtime, and ensure the long-term stable operation of equipment.

    Conclusion

    Automated cranes have become the core infrastructure of intelligent manufacturing material handling, which can effectively avoid operational risks, improve handling accuracy and efficiency, rely on intelligent control, data operation and maintenance capabilities to reduce long-term operating costs of enterprises, and help industrial handling digitize and upgrade safely.

    The upgrade of an enterprise needs to combine working conditions, needs and long-term planning to select the type reasonably to avoid waste of high configuration.Henan Mine Crane, a professional manufacturer, can provide customized solutions for bridge, gantry and automated cranes to meet various production scenarios and intelligent transformation needs.If you have any project plans, you can consult at any time to obtain exclusive plans and quotations.

    Henan Mine CraneDiscuss your requirements ↗
  • Aerospace vs Military Grade Crane Which is More Reliable

    Aerospace vs Military Grade Crane Which is More Reliable

    Aerospace vs Military Grade Crane Which is More Reliable

    In mission-critical lifting operations, reliability isn’t a nice-to-have, it’s the entire point of the equipment. A crane failure on an aircraft assembly line can damage a component worth millions of dollars. A crane failure at a forward military depot can stall an operation with no backup equipment for miles. Both scenarios demand exceptional performance, but they demand it in different ways.

    Aerospace cranes and military grade cranes are often mentioned in the same breath, as if they’re interchangeable premium tiers of lifting equipment. They aren’t. They’re designed around different operating environments, different mission requirements, and different definitions of what “failure” looks like. This guide compares their design philosophy, reliability standards, and application scenarios so buyers can choose the right solution rather than the more impressive-sounding label.

    Procurement teams frequently default to whichever label sounds more rigorous, assuming that military grade automatically means tougher, or that aerospace automatically means better engineered. In practice, both labels describe a bundle of design choices, testing regimes, and quality certifications tailored to a specific failure profile. A crane that excels at millimeter-accurate positioning inside a climate-controlled hangar may be a poor fit for a coastal naval depot exposed to salt spray and temperature swings, and vice versa. Understanding what each designation actually guarantees, rather than what it implies, is the first step toward specifying equipment that performs as expected over its full service life.

    What Is an Aerospace Crane?

    Henan Mine Crane manufactured aerospace crane is engineered around precision, stability, and cleanliness. In aircraft and spacecraft manufacturing, the crane isn’t just moving weight — it’s positioning components worth hundreds of thousands to millions of dollars with tolerances that leave almost no margin for error.

    Typical Applications

    • Aircraft manufacturing
    • Spacecraft assembly
    • Satellite production
    • Rocket integration facilities

    In each of these environments, the crane works in a tightly integrated production flow. When parts for fuselage sections, wing configurations, satellite buses, and rocket stages are typical of low production volumes (sometimes one of a kind), handling damage becomes very expensive and can itself cause delays to the entire program.

    Key Performance Requirements

    • High positional accuracy:because assembly operations dictates tolerances at a few millimeters, and realized at the final stages by means of VFD control and ultra-low creep speeds.
    • Smooth lifting motion:which uneven acceleration or deceleration may damage delicate composites, precision-machined surfaces, or sensitive avionics.
    • Low vibration:Essential for precision assembly and for sensitive sensor and optical equipment.
    • Cleanroom compatibility:Numerous aerospace and satellite cranes perform in classified cleanroom environments and FOD control is among the highest safety priorities.

    Beyond these baseline requirements, aerospace cranes are frequently expected to integrate directly with the surrounding production system. That can mean synchronizing with automated drilling and fastening equipment, logging every lift for quality traceability, or supporting tandem dual-hoist operations for long, flexible components like wing sections that can flex and amplify sway if motion isn’t carefully controlled. Because a single dropped fastener or a scuffed composite panel can ground an entire production line, the crane is treated less like a piece of material-handling equipment and more like a precision instrument embedded in the manufacturing process itself.

    What Is a Military Grade Crane?

    Henan Mine Crane manufactured military grade crane is engineered around durability and continuous operational readiness. Rather than optimizing for a controlled indoor environment, it’s built on the assumption that the operating environment itself is the primary threat , extreme heat, cold, humidity, corrosion, dust, and shock.

    Typical Applications

    • Military logistics
    • Ammunition handling
    • Naval bases
    • Vehicle maintenance depots
    • Missile assembly facilities

    These environments share a common thread: equipment failure isn’t just costly, it can directly affect mission readiness. A crane at a naval base or forward maintenance depot often has no immediate backup, so reliability under stress is non-negotiable.

    Key Performance Requirements

    • Heavy-duty operation: built for frequent, high-intensity lifting cycles over long service periods.
    • Shock resistance: structural components engineered to absorb mechanical shock without cracking or losing calibration.
    • Extreme weather capability: validated performance across desert heat, arctic cold, high humidity, and coastal salt exposure.
    • Rapid deployment: some military cranes are designed for mobile or semi-permanent installation in field conditions.
    • High durability: components selected for a long service life with minimal maintenance downtime, since military cranes commonly remain in service for 15–25 years.

    These requirements are rarely evaluated in isolation. A crane serving a naval base, for example, must simultaneously resist salt-air corrosion, operate reliably across a wide temperature band, and remain serviceable by technicians without specialized tooling, because in a deployed or forward-operating context, there may be no realistic option to wait weeks for a replacement part. This is why military procurement places heavy weight on standardized components and interchangeable spares across a fleet: a base with ten cranes from ten different configurations is a maintenance and readiness liability, while a standardized fleet simplifies training, spares inventory, and field repair.

    Aerospace Crane vs Military Grade Crane: Key Differences

    Design Philosophy: Precision vs Durability

    Aerospace cranes are engineered around precision, the ability to place a load exactly where it needs to be, repeatedly, without damaging it. Henan Mine Crane manufactured military grade cranes are engineered around durability, the ability to keep functioning at rated capacity after years of exposure to harsh conditions. Neither design philosophy is “better” in isolation; they solve different problems.

    Operating Environment

    Aerospace cranes typically work inside controlled manufacturing facilities, climate-controlled hangars, cleanrooms, and assembly halls where temperature, humidity, and airborne contaminants are already managed by the building itself. Because the facility handles environmental control, the crane’s engineering budget can be spent almost entirely on motion precision rather than ruggedization. Military grade cranes are built for harsh outdoor environments, including shipyards, desert bases, coastal installations, and forward operating locations where no such environmental control exists. Here, the crane itself has to be the resilient element, since there’s no building system compensating for temperature swings, blowing sand, or salt-laden air.

    Lifting Accuracy

    Aerospace cranes are held to tight positioning tolerances, often in the low single-digit millimeter range for major assembly operations, supported by anti-sway systems and micro-speed motion control. Some automated drilling and fastening operations demand even tighter positioning than general assembly work, pushing precision requirements further still. Military grade cranes are not typically specified against the same accuracy benchmarks, capacity, ruggedness, and uptime take priority over micron-level positioning. That doesn’t mean military cranes are imprecise; it means their engineering priorities are allocated differently, with accuracy sufficient for the task but not treated as the primary design driver.

    Load Capacity

    Both categories span a wide capacity range depending on application. Henan Mine Crane manufactured aerospace double girder cranes commonly range from 5–50 tonnes, with some final-assembly configurations exceeding that for large aircraft sections, and spans of 20–50 meters or more are typical across major assembly bays. Component weight alone rarely tells the whole story, either, lifting attachments such as spreader beams, cradles, and vacuum systems can add significant additional weight, which is why aerospace facilities often specify crane capacity at 1.5–2x the heaviest single component to leave headroom for tooling and future production requirements. Military cranes handling missile containers, ship modules, or armored vehicles often require higher capacities and longer spans to bridge wide hangars, shipyards, or missile silos, and large-span configurations exceeding 70 meters are not unusual for facilities handling entire ship sections or long-range missile systems.

    Environmental Resistance

    This is where the two categories diverge most clearly:

    • Temperature: military cranes are tested across extreme heat and cold ranges; aerospace cranes generally assume climate-controlled conditions.
    • Dust:military cranes must resist sand and dust ingress in field deployments; aerospace cranes rely on facility-level contamination control plus onboard FOD prevention.
    • Humidity: military cranes are validated for high-humidity and monsoon-type conditions; aerospace facilities typically manage humidity through HVAC systems.
    • Corrosion: military cranes near coastal or naval environments require enhanced corrosion-resistant coatings; aerospace cranes need corrosion resistance appropriate to indoor industrial use.
    • Shock: military cranes are engineered to absorb mechanical shock and vibration from transport and field use; aerospace cranes are engineered to minimize vibration transmitted to the load itself.

    Which Crane Offers Better Reliability?

    Reliability in Precision Manufacturing

    In an aerospace assembly environment, the biggest reliability risk isn’t a dramatic mechanical failure , it’s a precision failure: a slight drift in positioning accuracy, a jerky start-stop motion, or excess load sway that damages a component or forces costly rework. Unlike a catastrophic breakdown, a precision failure can go unnoticed until quality inspection flags an out-of-tolerance part, by which point the cost has already been incurred. Aerospace cranes are optimized specifically to minimize this risk, which is why reliability in this context is measured largely through positioning repeatability over the crane’s operating life rather than through simple uptime percentages.

    Reliability in Harsh Field Operations

    In a military logistics or depot environment, the biggest reliability risk is unplanned downtime in a location with limited support infrastructure. A crane failure at a forward base, naval yard, or other critical logistics hub can cause delays with potentially strategic effects which in commercial markets are usually mitigated by back-up units or help on the same day but commercial cranes weren’t designed for the strategic pressures of the U.S. military, requiring instead hardened construction, redundant parts, and structural endurance, and readiness indicated by mission-capable rates rather than accuracy of placement.

    overhead crane

    Maintenance Requirements

    Henan Mine Crane Factory supply aerospace cranes generally require regular calibration checks to preserve positioning accuracy, alongside standard mechanical maintenance. Drift in a positioning sensor or a slight change in drive response can be invisible day-to-day but compound into measurable placement error over months of use, so calibration schedules tend to be tighter and more frequent than in general industrial settings. Military grade cranes are designed to minimize maintenance frequency altogether, since field maintenance access is often limited , this typically means simpler, more standardized components that are easier to service or swap in the field, along with design choices that favor mechanical robustness over sensor-dependent precision systems that could be harder to repair without specialized technicians.

    Expected Service Life

    Military grade cranes are frequently specified with a 15–25 year field service expectation. Aerospace cranes are often tied to the lifecycle of a specific production program, though well-maintained units can remain in service for decades in stable facility environments.

    Failure Risk Analysis

    Failure Mode Aerospace Crane Risk Military Grade Crane Risk
    Precision drift damaging a component Primary concern Secondary concern
    Structural failure under extreme temperature Low (controlled environment) Primary concern
    Corrosion-related degradation Low to moderate Primary concern (coastal/field use)
    Unplanned downtime with no backup equipment Moderate (production delay) High (mission impact)
    Contamination affecting sensitive components Primary concern (FOD) Low priority

    Bottom line: neither crane type is universally more reliable. Aerospace cranes are more reliable for precision handling in controlled environments. Military grade cranes are more reliable for sustained operation in harsh, unpredictable field conditions. The right answer depends entirely on which failure mode your operation is most exposed to.

    Core Technologies That Improve Crane Reliability

    Regardless of grade, several core technologies consistently improve reliability across both categories:

    Anti-Sway Control Systems

    Electronic systems that predict and counteract load swing, reducing sway significantly during transport and positioning , critical for both delicate aerospace components and awkwardly shaped military cargo like missile containers.

    Variable Frequency Drives (VFD)

    Stepless speed control, which connoisseurs would use to smooth acceleration and deceleration, remains one of the early VFDs’s virtues. Jerky contactor controlled drive  has long been relegated to the history books. Aerospace precision work and the mechanical strength stress of military Duty cranes gain from this contribution.

    Intelligent Load Monitoring

    Automated, load-dependent load weighing and handling systems that automatically adapt lifting speed to load weight, enabling uniform handling regardless of component mass, and activating overload warning systems well in advance of force overload conditions becoming safety incidents.

    Redundant Safety Protection

    Secondary braking systems, overspeed protection and load-arrest devices add an additional cushion critical in military missions and aerospace handling that can’t afford a single point of failure.

    Predictive Maintenance

    Monitoring motor temperature, vibration signatures and duty cycles electronically sensors makes it easier for maintenance teams to detect trouble before failure. This results in longer service life for the tool in question and less unplanned downtime in either environment. In an aerospace plant, a monitor may catch a bearing wear condition and prevent an offsetting during a position adjustment. In a military depot provide early warning on a motor about to hit end-of-life measures prior to unexpected failure on active duty.

    Remote Condition Monitoring

    Cloud-connected or networked monitoring systems that report operating hours, fault codes, and performance data, particularly valuable for military installations where technical support may not be on-site, and for multi-crane aerospace facilities coordinating complex lifts from a central control room. For defense applications, remote monitoring also supports fleet-wide readiness reporting, allowing logistics planners to see at a glance which units at which bases require service before they become a mission risk.

    Choosing the Right Crane for Different Industries

    Aerospace Manufacturing

    Prioritize precision motion control, FOD prevention, and AS9100-certified manufacturing quality. Henan Mine Crane Factory supply double girder overhead cranes with VFD control are the standard workhorse for assembly hall operations. Beyond the crane itself, evaluate how well the system integrates with existing jigs, fixtures, and automated tooling — a crane specified in isolation from the rest of the production line often ends up as a bottleneck rather than an asset. Facilities handling composite structures should also confirm the crane’s load-swing performance under partial loads, since uneven or asymmetric components behave differently in transit than uniform loads and can introduce unexpected sway if the anti-sway system isn’t tuned for that load profile.

    Defense Industry

    Prioritize MIL-STD-810/461 compliance, structural durability, and long-term parts standardization across a fleet. Facilities producing military aircraft often require dual compliance with both aerospace and military standards, since the same crane may need to handle a fuselage section with aerospace-level precision while also surviving a coastal or high-vibration environment. Procurement teams in this segment should also weigh interoperability requirements — NATO and allied operations often call for CE marking alongside MIL-STD compliance — and should factor multi-decade support contracts into supplier selection, since defense equipment is expected to remain serviceable long after commercial products of the same era have been discontinued.

    Shipbuilding

    Prioritize large-span capacity, marine corrosion resistance, and shock tolerance. Gantry cranes are popular in shipbuilding shops since they can traverse large open outdoor distances and there are most likely “requirements for specialized coatings and sealed electrical components”, given how they will be subjected to salt air and water all day long. In addition, work at shipbuilding shops often requires uneven, unbalanced loads, such as hull sections or superstructure blocks, so tandem lifting capability and on-the-fly weight-centering/center-of-gravity monitoring should be valued equally with maximum capacity.

    Nuclear Facilities

    In view of the high cost of a damage or accident, emphasis needs to be placed on redundant safety systems, accurate load control and documented certification and inspection. Crane was always a subject of extra regulation over and above normal industrial or defense certification in this environment. Some or all of the following may be required; more regular proof-load testing; more exacting operator certification; utilization of radiation tolerant components; remote operated cranes.

    Heavy Equipment Manufacturing

    Make sure the duty cycle and load capacity requirements take precedence over positioning accuracy and tight tolerances, as the products in this environment are generally tougher and not affected by small handling differences as aerospace parts are. This category of environment is not unusual for cranes to operate at higher duty cycles than aerospace or defense environments, and many Center of Manufacturing and Assembly/Facilities Engineering Management (CMAA/ FEM) duty classifications and wear life requirements on hoist and trolley components should be taken into account during specification.

    Common Crane Types Used in Aerospace and Military Industries

    Double Girder Overhead Crane

    The workhorse of aerospace assembly facilities and military maintenance depots. Delivers the hook height and stability demanded for manipulation of large components, in capacities of 5 50 tonnes in most cases. With a twin-girder set-up, the machine offers superior torsional stability over a single-girder, a benefit that comes into play when manipulating long, asymmetrical loads such as wing sections or vehicle hulls, and this type of Crane commonly offers dual-hoist configurations for tandem lifting of really long or heavy components.

    Single Girder Overhead Crane

    Ideal for lighter lifting applications, and smaller facilities, providing a smaller footprint and easier fit into lower ceiling height spaces, these systems are practical for smaller maintenance bays, parts storage areas or secondary work cells where the full double girder capacity isn’t needed, and their lower cost and simpler design can make them more economical where numerous, lower use lifting points are needed in a facility.

    Gantry Crane

    Gantry cranes are supported by legs instead of an overhead structure and are frequently used in shipyards and outside military facilities, when it is undesirable to have an overhead runway defined. Because they are self-supported they are often used at forward bases on a temporary/semi-permanent basis where the construction of a full overhead runway is not justified.

    Jib Crane

    Jib Crane (Local use): Localized lifting of small payloads. Used where a dedicated overhead crane is not justified, e.g. assembly bays and workplace areas. In aerospace applications, many local-purpose jib cranes are used at individual assembly bays for small job handling, so that the overhead crane for structural lifts can be spared.

    Explosion-Proof Crane

    Infamous for the creation of available sparks, this is an enameled, electrically-sealed unit required in munitions handling plants and combustible atmospheres. Typically terminating in a sealed electrical enclosure, these specialized units are manufactured with non-sparking construction throughout the entire hoist and control system, since the slightest electrical short could be the difference between survival or destruction in a munitions handling application. Explosion proof classifications are generally given according to hazard zone as well as the material class, and specifications should begin with a hazard assessment of a plant, rather than simply an explosion proof label.

    Intelligent Crane Systems

    Cranes integrated with anti-sway control, load monitoring, and remote diagnostics , increasingly used in both satellite assembly (for precision) and military logistics (for remote condition monitoring). These systems increasingly incorporate programmable motion profiles that let operators save and recall precise lift sequences for repeated operations, along with data logging that supports both aerospace traceability requirements and military fleet-readiness reporting from a single underlying platform.

    Application Comparison Table

    Industry Recommended Crane Type Primary Advantages
    Aerospace Manufacturing Double Girder Overhead Crane High precision, smooth positioning
    Satellite Assembly Intelligent Overhead Crane Anti-sway, precise load control
    Military Maintenance Double Girder Crane Heavy-duty lifting, durability
    Ammunition Facilities Explosion-Proof Crane Enhanced operational safety
    Naval Shipyards Gantry Crane Large-span heavy lifting

    Henan Mine Crane Factory Custom

    Aerospace and military applications demand different definitions of reliability, but both require cranes engineered for long-term performance, operational safety, and application-specific requirements. Whether the priority is millimeter-level positioning in aerospace manufacturing or dependable operation in harsh military environments, selecting the right crane depends on matching the equipment to the working conditions, duty cycle, environmental challenges, and reliability expectations of the project.

    As a professional crane manufacturer with extensive experience in customized material handling solutions, Henan Mine Crane Factory provides overhead cranes, gantry cranes, intelligent crane systems, and other heavy-duty lifting equipment for demanding industries, including aerospace, defense-related manufacturing, shipbuilding, steel, and energy. Backed by strong R&D capabilities, rigorous quality control, and full lifecycle service, we help customers develop reliable lifting solutions that improve productivity, reduce lifecycle costs, and support safe, efficient operations for years to come.

    Henan Mine CraneDiscuss your requirements ↗