Henan Mine Crane · Engineered Coil Handling Systems for Automotive Production
Coil Handling Cranes for the Automotive Industry
Overhead cranes with C-hooks, coil tongs and magnetic beams for steel and aluminium coil storage, blanking line feed, decoiler service and coil transfer in automotive stamping and rolling plants.
Henan Mine Crane engineers automotive coil handling cranes around the coil schedule, surface class, eye orientation, storage geometry and cycle rate of each line. Each proposal defines the crane, attachment, power and control system, safety functions, electrical boundary, documentation, delivery and requested site services.
ATTACHMENT OPTIONS
C-Hook, Tong & Magnet
TYPICAL COIL WEIGHT
5 t – 25 t
CRANE CAPACITY CLASS
5 t – 50 t
COIL SERVICE DUTY
A5 – A7 Continuous
What Coil Handling in an Automotive Plant Involves
A coil handling crane for the automotive industry moves steel and aluminium coils between storage, preparation and the press lines that turn them into body panels. In a typical stamping operation, coils weigh from roughly 5 to 25 tonnes, arrive eye-vertical or eye-horizontal, sit in racks or on saddles, and feed blanking lines and decoilers that run to the rhythm of the press shop. The crane is the link between every one of those positions, and its cycle is tied directly to line demand rather than to a schedule of its own.
What separates automotive coil handling from general coil service is the surface. A large share of automotive sheet carries exposed or pre-coated finishes destined for visible body panels, where any mark on the coil surface becomes a defect in a stamped part. The crane, the C-hook or tong that carries the coil, the saddle it rests on and the way it is set down all have to preserve the surface class of the material — with protective linings, controlled contact pressure and smooth acceleration and deceleration engineered in from the start.
The attachment defines the machine. C-hooks and mechanical tongs handle any material including non-ferrous and coated coil; magnetic beams pick ferrous coils at speed but depend on material, temperature and surface condition. Rotating beams and slewing trolleys turn coils between eye orientations. Every attachment has its own rated certification as a below-the-hook lifting device, and its weight plus the coil weight must be carried inside the rated capacity of the crane.
Henan Mine Crane supplies automotive coil handling systems as engineered packages: the crane structure and machinery, the C-hook, tong or magnetic attachment with its power and control, storage saddle and rack interfaces, safety functions and documentation — configured against the coil schedule and cycle rate of the specific plant.
Where Coil Cranes Work in an Automotive Plant
Coil Storage and Rack Handling
Cranes place and retrieve coils from storage racks, saddles and stacked positions. Placement accuracy protects both the coil surface and the rack structure, and the storage layout defines the coverage the crane has to deliver.
Blanking Line Feed
Coils are delivered to blanking and cut-to-length lines in the sequence the line calls for. Cycle rate at the line sets the duty class of the crane — continuous blanking service is among the most demanding in the plant.
Press Shop Decoiler Service
Loading coils onto decoilers and mandrels combines heavy loads with tight positioning. Eye orientation, mandrel alignment and gentle set-down decide whether the line threads up quickly or loses time every coil change.
Coil Transfer Between Bays
Coils move from receiving to storage, from storage to preparation and between bays. Transfer cranes and where required gantry links carry these moves, with eye rotation where the receiving position differs from the storage orientation.
Return and Residual Coil Handling
Part-used and residual coils return to storage with documented identity and surface condition. The same cranes handle these lighter but more frequent moves, often across a wider area of the coil yard.
Scrap and Skeleton Handling
Blanking skeletons and scrap return from the presses. Where the same bay handles both, magnet or grab duty is specified alongside the coil attachment on a dual-purpose configuration with the higher of the two duty classes.
Attachments and Configurations for Coil Service
The coil defines the attachment, and the attachment defines the crane. Each option below earns its place under specific material, surface and cycle conditions found in automotive plants.
The C-hook is the standard device for coil handling in stamping plants. It enters the coil eye, carries the coil on its saddle, and works with any material — ferrous, non-ferrous, coated or bare. Lined contact surfaces and controlled set-down protect the finish, and no power supply is needed at the hook. Coil tongs grip the outside diameter instead of the eye, for narrow coils, tight rack positions or where the eye is not accessible.
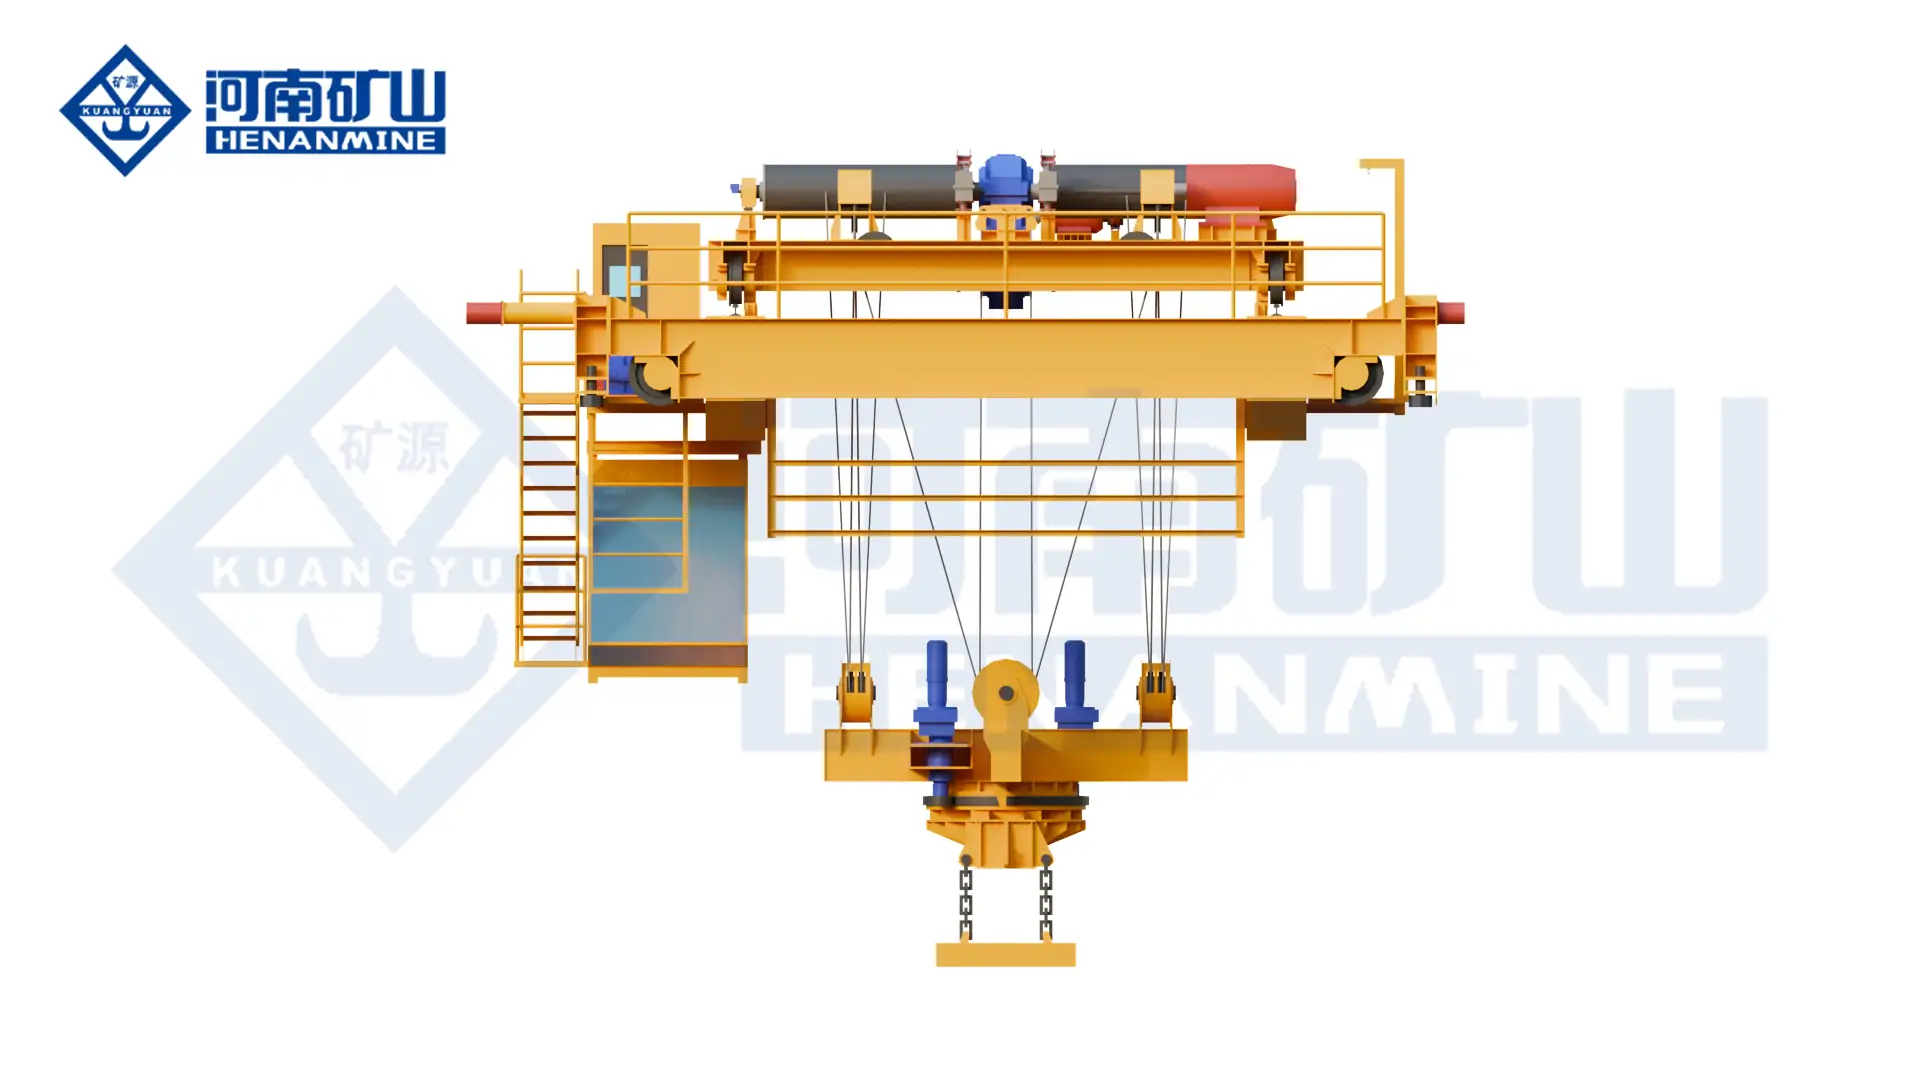
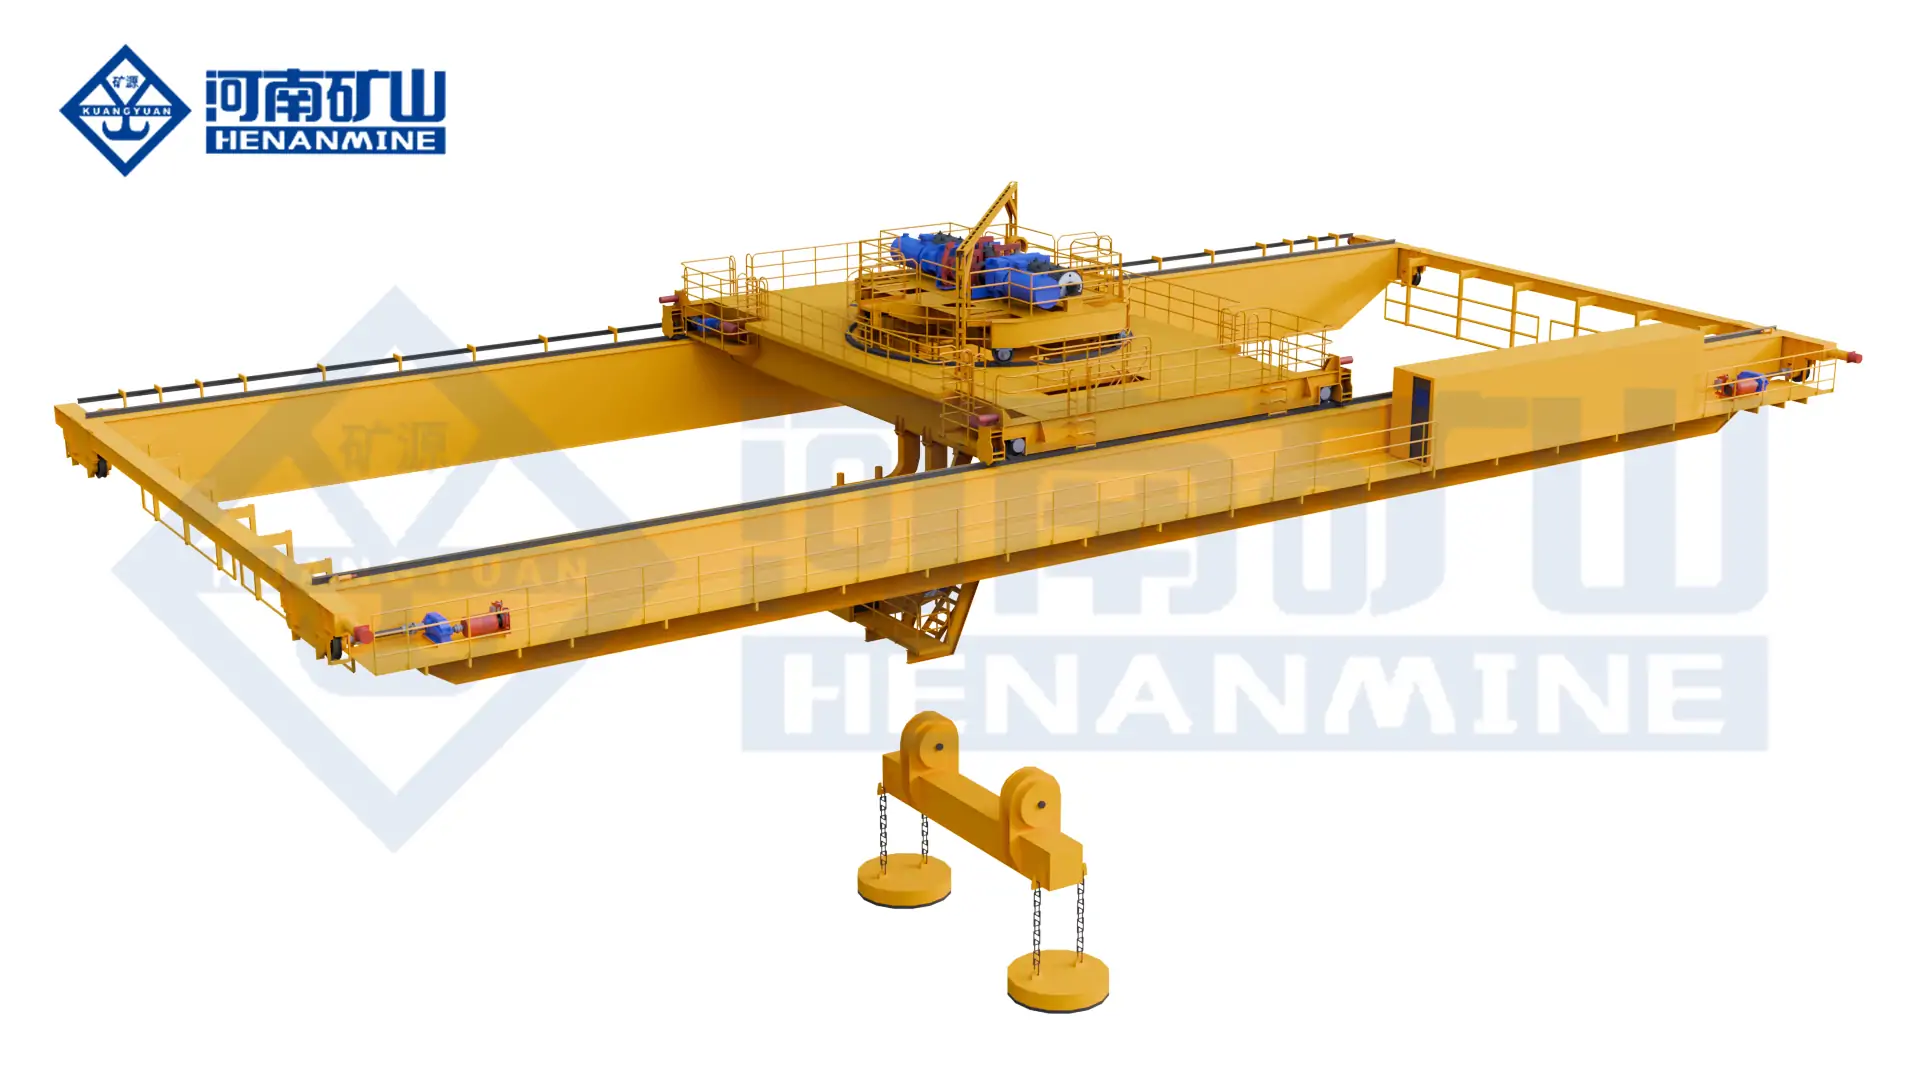
Magnetic beams pick ferrous coils by direct magnetic contact, in oval or rectangular layouts matched to the coil orientation, and cycle faster than mechanical devices because there is no hook to place. They depend on material, temperature and surface condition, and they need magnet power, control and a defined release procedure. Rotating magnetic beams and slewing-trolley cranes add rotation between eye orientations, so a coil received eye-vertical can be stored or delivered eye-horizontal without a separate handling step.
The crane under the attachment is typically a double girder bridge crane — the capacity class, hook approach and stiffness that coil service needs — with variable frequency travel control for smooth acceleration and micro-speed positioning on saddles and mandrels. Single girder cranes cover light coil and auxiliary duty. Every attachment is rated and certified as a below-the-hook lifting device, separately from the crane certification.
Coil Handling Crane Selection Considerations
Selection starts with the coil schedule — the full list of coils the plant actually handles — and works outward to the attachment, the duty class and the building. These parameters establish the specification a quotation must be built against.
01 · Coil Schedule and Weight
List every coil by weight, width, outer diameter and eye diameter. The heaviest coil plus the attachment tare sets the rated capacity — a 25 t coil on a 5 t C-hook demands a crane rated above 30 t, not 25 t.
02 · Material and Surface Class
Ferrous, non-ferrous, coated or exposed surface — the material decides between magnetic and mechanical attachment, and the surface class sets the lining, contact pressure and handling limits that protect the finish.
03 · Eye Orientation and Rotation
Coils arrive eye-vertical or eye-horizontal, and storage, decoiler and rack positions do not always match. Where orientation changes, a rotating beam or slewing trolley removes a whole handling step from the cycle.
04 · Cycle Rate and Duty Class
Coils per hour, shift pattern and travel distances convert into mechanism classifications. Continuous blanking and decoiler feed duty typically requires A6–A7; intermittent warehouse duty may justify A5. Duty class set too low is the most common cause of early coil crane failure.
05 · Storage Geometry
Rack positions, saddle types, stacking heights and aisle widths define the hook path and placement accuracy the crane must achieve. The storage layout is agreed with the crane specification, not after it.
06 · Magnet Power and Control
Magnetic attachments need their power supply, controller, cable management and a defined behaviour on power loss. Battery backup and monitored release are specified where the coil schedule justifies them.
07 · Automation and Line Integration
Coil identification, position feedback, anti-sway, rack interlocks and communication with the line or storage system turn a crane into part of the material flow. The functional scope belongs in the specification, not in later site improvisation.
08 · Attachment Certification and Boundary
Below-the-hook devices carry their own rated certification, separate from the crane’s declaration. Runway interface, installation, testing, spares and documentation are assigned in writing before quotations are compared.
Coil Handling Configurations Compared
The correct attachment and crane combination handles the full coil schedule at the required cycle rate without transferring damage risk into the material or unnecessary cost into the plant.
| Configuration | Coil Compatibility | Handling Character | Surface Risk | Critical Limit |
|---|---|---|---|---|
| Double girder crane with C-hook | All materials, coated and non-ferrous included | Hook into eye, controlled saddle placement | Low — lined contact, no power at the hook | Hook placement takes operator skill and time |
| Crane with coil tong | All materials, narrow coils and tight positions | Grips the outside diameter at defined points | Controlled with padded contact faces | Grip range must match the coil schedule |
| Crane with magnetic beam | Ferrous coils within temperature and surface limits | Fast pick and release, high cycle capability | Marking risk on finished surfaces | Needs magnet power, control and defined release behaviour |
| Rotating magnetic beam crane | Ferrous coils needing orientation change | Lifts and turns between eye orientations in one cycle | Marking risk on finished surfaces | Rotation mechanism adds tare weight and maintenance |
| Single girder crane, light coil duty | Light coils, return coils, auxiliary handling | Economical coverage with C-hook or light tong | Low at moderate cycles | Capacity and duty ceiling limits service range |
| Dual purpose coil and scrap crane | Ferrous coils plus skeleton and scrap duty in one bay | Coil attachment plus magnet or grab capability | Managed by attachment change procedure | Rated to the heavier combination and higher duty class |
Coil Handling Crane Technical Specification Framework
Henan Mine Crane maintains several crane families applied to coil handling service. The ranges below support preliminary configuration and are not guaranteed combinations. Final capacity, span, lift, working class, speeds and wheel loads are confirmed on the approved technical schedule and general arrangement drawing, together with the rated attachment.
| Product Family | Published Capacity Position | Published Span Position | Lifting Height Position | Working Class Position | Primary Coil Handling Use |
|---|---|---|---|---|---|
| Bottom-rotating electromagnetic hanging beam crane | Project-configured around the coil schedule | 10.5–31.5 m or project-defined | 6–20 m or customized | A6–A7 by cycle profile | Ferrous coil handling with rotation and alignment |
| Electromagnetic overhead crane (QC family) | 5–50 t | 10.5–31.5 m | 6–30 m | A6–A7 | High-frequency ferrous coil transfer and line feed |
| Upper-rotating magnetic overhead crane | Model-specific, slewing-trolley configuration | 10.5–31.5 m or project-defined | 6–20 m or customized | A6–A7 | Coil positioning at multiple angles and orientations |
| Double girder bridge crane with C-hook | 5–50 t class including attachment tare | 10.5–31.5 m | 6–30 m or project-defined | A5–A6 by cycle profile | Coated, non-ferrous and mixed coil schedules |
| Single girder crane for light coil duty | 1–20 t across the family | 7.5–28.5 m | 6–18 m or project-defined | A3–A5 | Light and return coils, auxiliary handling |
| Metallurgical bridge crane | 5–200 t | Project-defined | Project-defined | A6–A8 | Heavy coil service integrated with rolling and steelmaking |
A capacity shown within one family does not confirm suitability at every span, lift or duty, and attachment tare weight is always carried inside the rated capacity. Coated-surface coils, high cycle counts and automation require project-specific calculation and verification.
Surface Protection and Duty Reliability
Two failure modes dominate coil handling complaints: marked surfaces on material destined for visible panels, and cranes that were specified one duty class below the service they actually run. Both are engineering decisions, and both are fixed in the specification.
Classified Surface Handling
The surface class of each coil family sets the permitted contact areas, lining materials, pressure limits and acceleration curves. Exposed and pre-coated material is handled to a different standard than black steel — by design, not by operator care.
Duty Class From the Cycle
Continuous blanking and decoiler feed service typically requires A6–A7 mechanisms and structure; intermittent warehouse work may justify A5. A general-duty crane running continuous coil cycles consumes its design life in a fraction of the rated period.
Controlled Set-Down
Variable frequency travel with micro-speed steps and anti-sway behaviour places coils on saddles and mandrels without shock. On decoiler loading, positioning accuracy converts directly into line uptime every coil change.
Attachment and Documentation
Below-the-hook devices carry their own rated certification. Structural calculations, test reports and acceptance criteria support commissioning and the plant’s audit systems, with the documentation scope agreed before manufacture.
Engineering and Supply Scope for Coil Handling Projects
A coil handling project typically defines the crane and the attachment together, as one lifting system: the bridge crane platform, the C-hook, tong or magnetic beam sized to the coil schedule, the magnet power and control equipment where applicable, the saddle and rack interfaces, and the storage layout the crane has to serve. Henan Mine Crane engineers the package against the full coil list, the cycle rate and the surface classes of the specific plant, so the attachment, duty class and control behaviour come from data instead of assumptions.
A complete supply definition states the crane structure and machinery, the rated attachment with its certification, the control and positioning functions, the runway interface, safety functions, the overload and acceptance testing regime, and the delivery, installation and commissioning responsibilities. Automation scope — coil identification, position feedback, rack interlocks and line communication — is defined in the same functional specification when the plant requires it.
Standard crane configurations are typically delivered within 30 to 45 days after drawing approval. Engineered coil handling systems with special attachments, rotation or automation run on confirmed project schedules agreed before production starts.
TYPICAL AUTO COIL WEIGHT
5 t – 25 t
ATTACHMENT OPTIONS
C-Hook, Tong, Magnet
STANDARD DELIVERY
30 – 45 Days
ENGINEERED DUTY RANGE
A5 – A7 Coil Service
Coil Handling Crane Price Reference
Current market positions for Chinese-manufactured crane equipment, expressed as indicative ranges. An equipment price covers the crane ex-works; attachment, runway, freight, duty, installation and commissioning are added separately and defined in the supply boundary.
| Crane and Attachment Scope | Typical Capacity | Indicative Price Position | What Moves the Number |
|---|---|---|---|
| Double girder crane for coil service (equipment only) | 10–20 t | US$12,000 – 40,000 | Span, lift, speed control level — before attachment |
| Double girder EOT with C-hook or coil tong | 10–32 t | US$35,000 – 120,000 | Duty class to M5+, attachment rating and certification |
| Heavy coil handling crane | 20–50 t | US$50,000 – 80,000+ | Span, duty, slow-speed and positioning control |
| C-hook attachment | 3.2–32 t device rating | US$650 – 5,000 (China sourcing); premium units to US$13,000 | Device rating, coil width, lining, origin and certification |
| Magnetic beam or coil tong attachment | Project-rated | US$8,000 – 30,000 | Magnet layout, rotation, power and control scope |
| Automation and installed system | On project scope | Project quotation; freight, duty and installation typically +20 – 50 % on FOB | Positioning, identification, interlocks, site services |
Comparing offers on a crane price alone understates the decision. Normalize every quotation to the same boundary — rated capacity including attachment tare, span, lift, duty class, speed control, attachment certification, conductor systems, installation, testing and documentation — before comparing numbers. A complete installed coil handling system typically lands well above the ex-works equipment figure.
Quote Information and Frequently Asked Questions
A complete enquiry should provide the coil schedule with weights, widths and eye dimensions, material and surface classes, eye orientations at each position, cycle rate, storage and line geometry, power supply, destination and the required supply boundary.
Coil and Material Data
Coil weights, widths, outer and eye diameters, material, surface class, eye orientation at every position and any rotation requirement between them.
Storage and Line Geometry
Rack and saddle layout, stacking heights, span or rail centers, hook heights, decoiler and blanking line positions, and the coverage each handling point requires.
Cycle and Duty Data
Coils per hour per line, shift pattern, travel distances, load spectrum and any automation or line-integration requirements.
Attachment and Commercial Data
Preferred attachment type, required certification, power supply, destination and Incoterm, installation responsibility, spares and requested delivery schedule.
What crane handles coils in an automotive plant?
Double girder bridge cranes with C-hooks or coil tongs are the standard configuration for moving coils between storage, blanking lines and decoilers. Magnetic beam cranes handle ferrous coils at higher cycle rates, and rotating beams or slewing-trolley cranes add orientation changes between eye positions.
C-hook, tong or magnet — which one for automotive coils?
C-hooks and tongs handle every material including coated and non-ferrous coil with lined, controlled contact. Magnets cycle faster but only lift ferrous material and carry marking risk on exposed surfaces. Many automotive plants run C-hooks for surface-critical coil and magnets for black steel and scrap duty.
Does the C-hook weight count towards crane capacity?
Yes. Rated capacity covers the total suspended load — the coil plus the hook, tong, beam, rotator and every interface below the crane hook. A 25 t coil on a 5 t C-hook requires a crane rated above 30 t, not 25 t.
How much does an automotive coil handling crane cost?
A 10–20 t double girder crane for coil service sits roughly between US$12,000 and 40,000 as equipment, before the attachment and special controls. Complete coil handling configurations with rated C-hooks or tongs typically run US$35,000–120,000, and heavy 20–50 t coil systems from about US$50,000. Freight, duty and installation typically add 20–50 % on top.
What duty class does coil service need?
Continuous blanking and decoiler feed duty typically requires A6–A7 mechanisms and structure; intermittent warehouse duty may justify A5. Duty class is calculated from the measured cycle profile — lifts per hour, load spectrum and travel distances — not from tonnage alone.
Can coil handling cranes be automated?
Yes. Position feedback, anti-sway, coil identification, rack and line interlocks and communication with storage or line control systems are integrated within a defined functional specification. Automation scope is quoted per project against the actual coil flow.
Related Crane Products for Coil Handling Service
Product selection follows the approved coil schedule, surface classes, cycle rate and storage geometry. Each linked model represents a separate configuration platform.
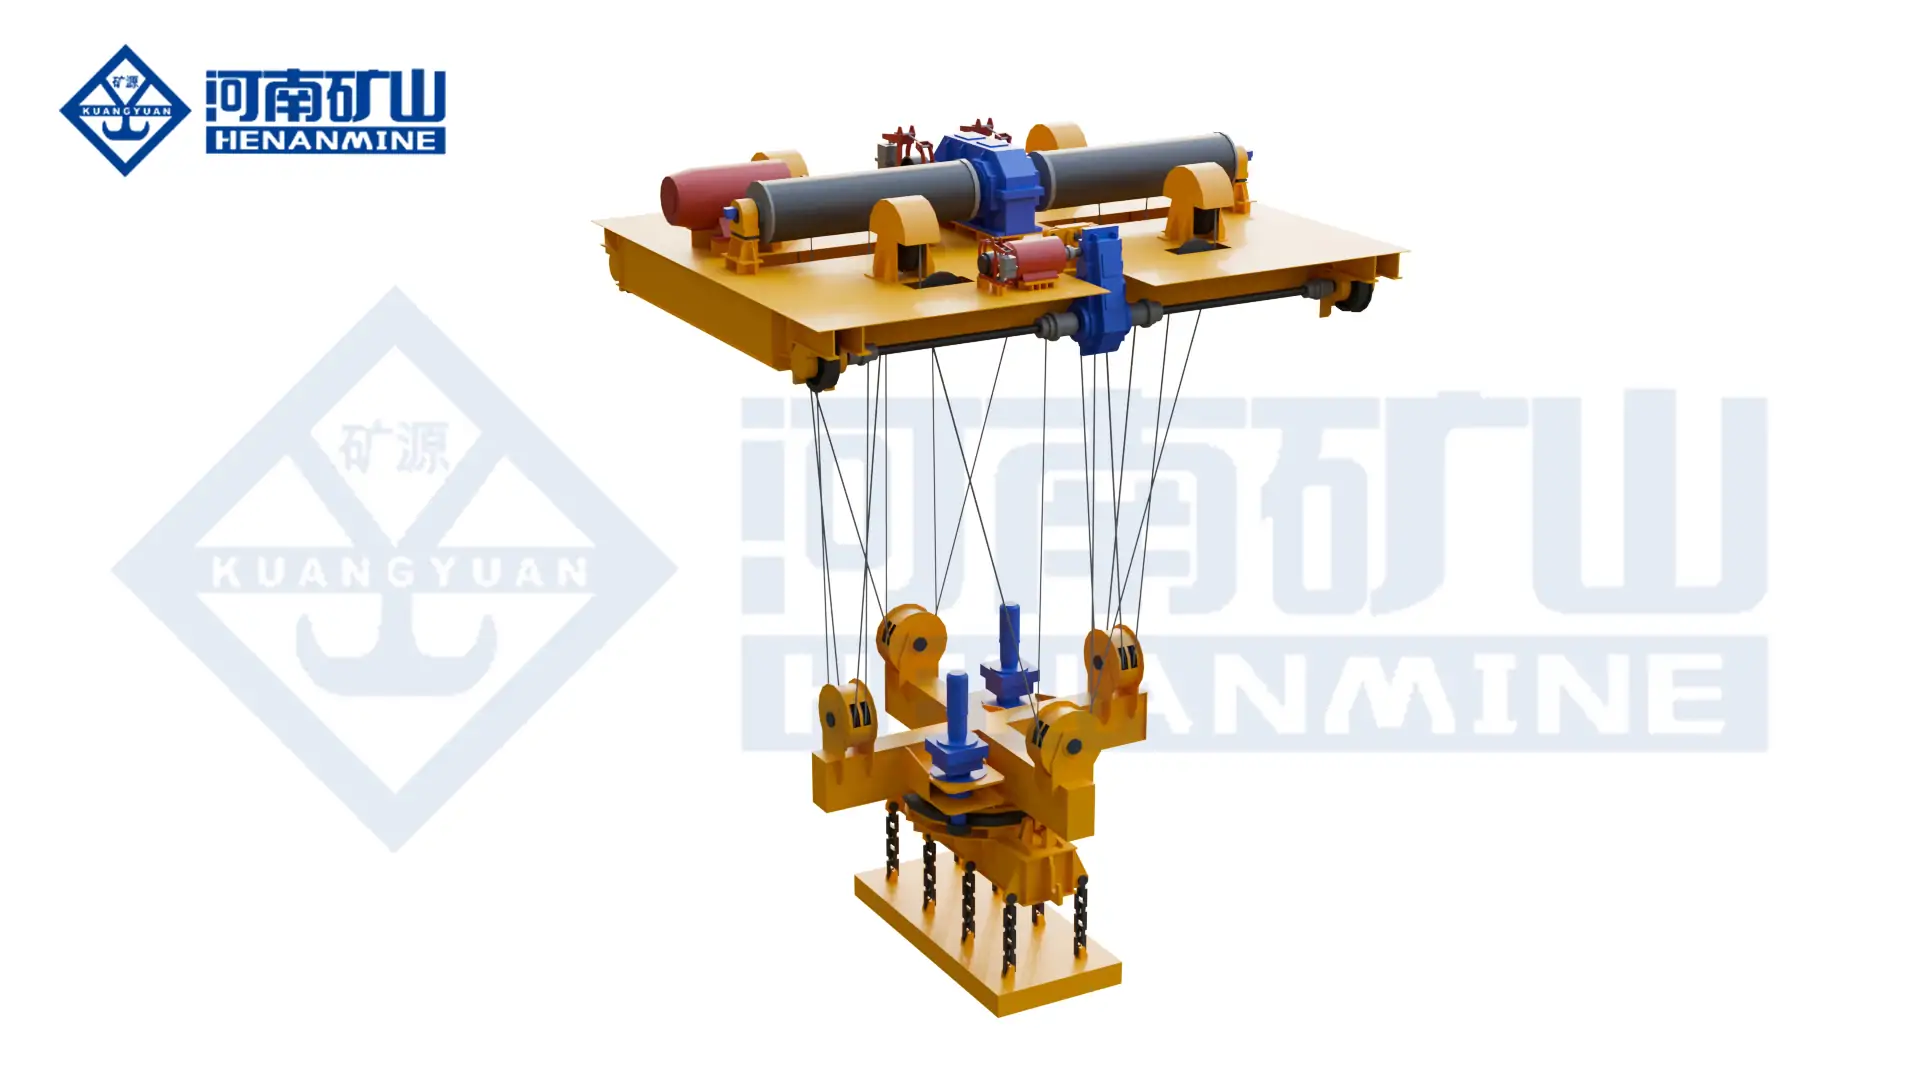
Electromagnetic Hanging Crane
Under-rotating magnetic beam crane for ferrous coil handling with rotation and alignment between storage and line positions.
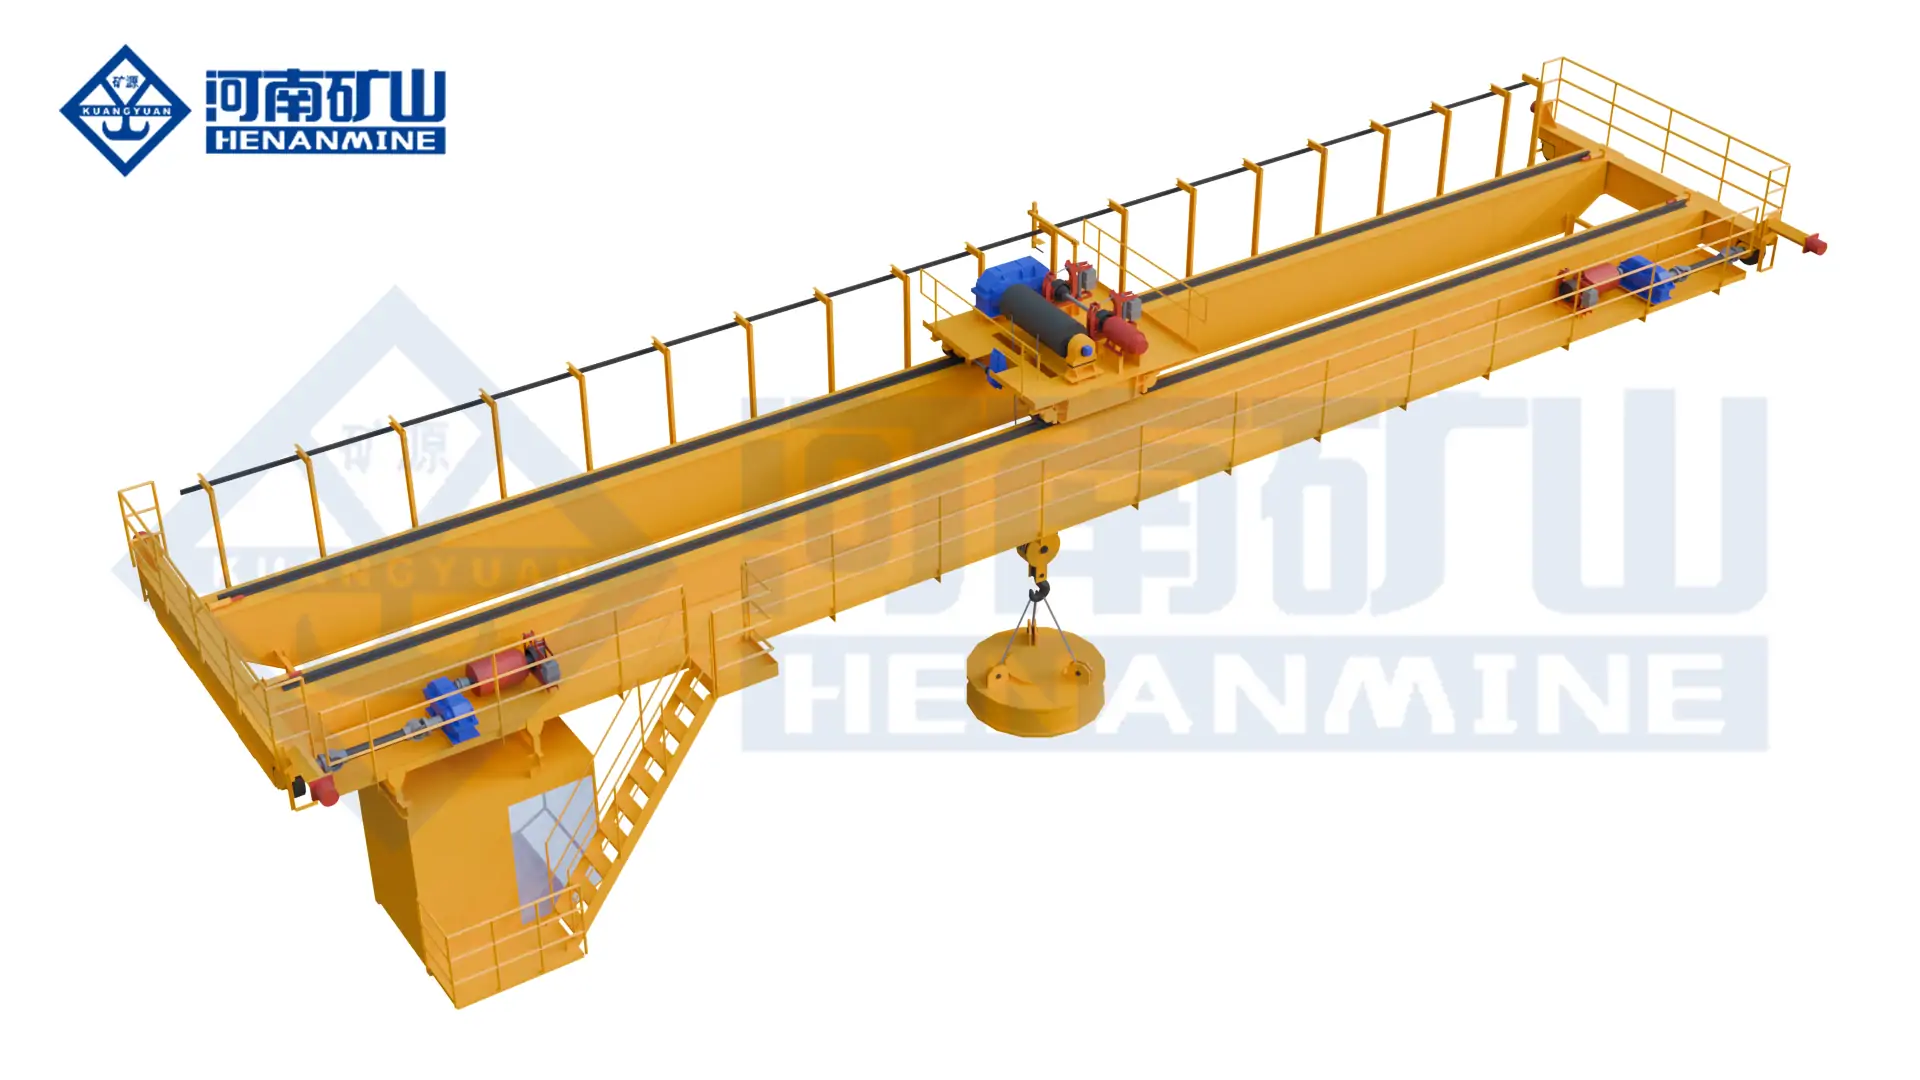
Electromagnetic Bridge Crane
Magnetic overhead crane platform, 5–50 t, for high-frequency ferrous coil transfer and line feed duty.
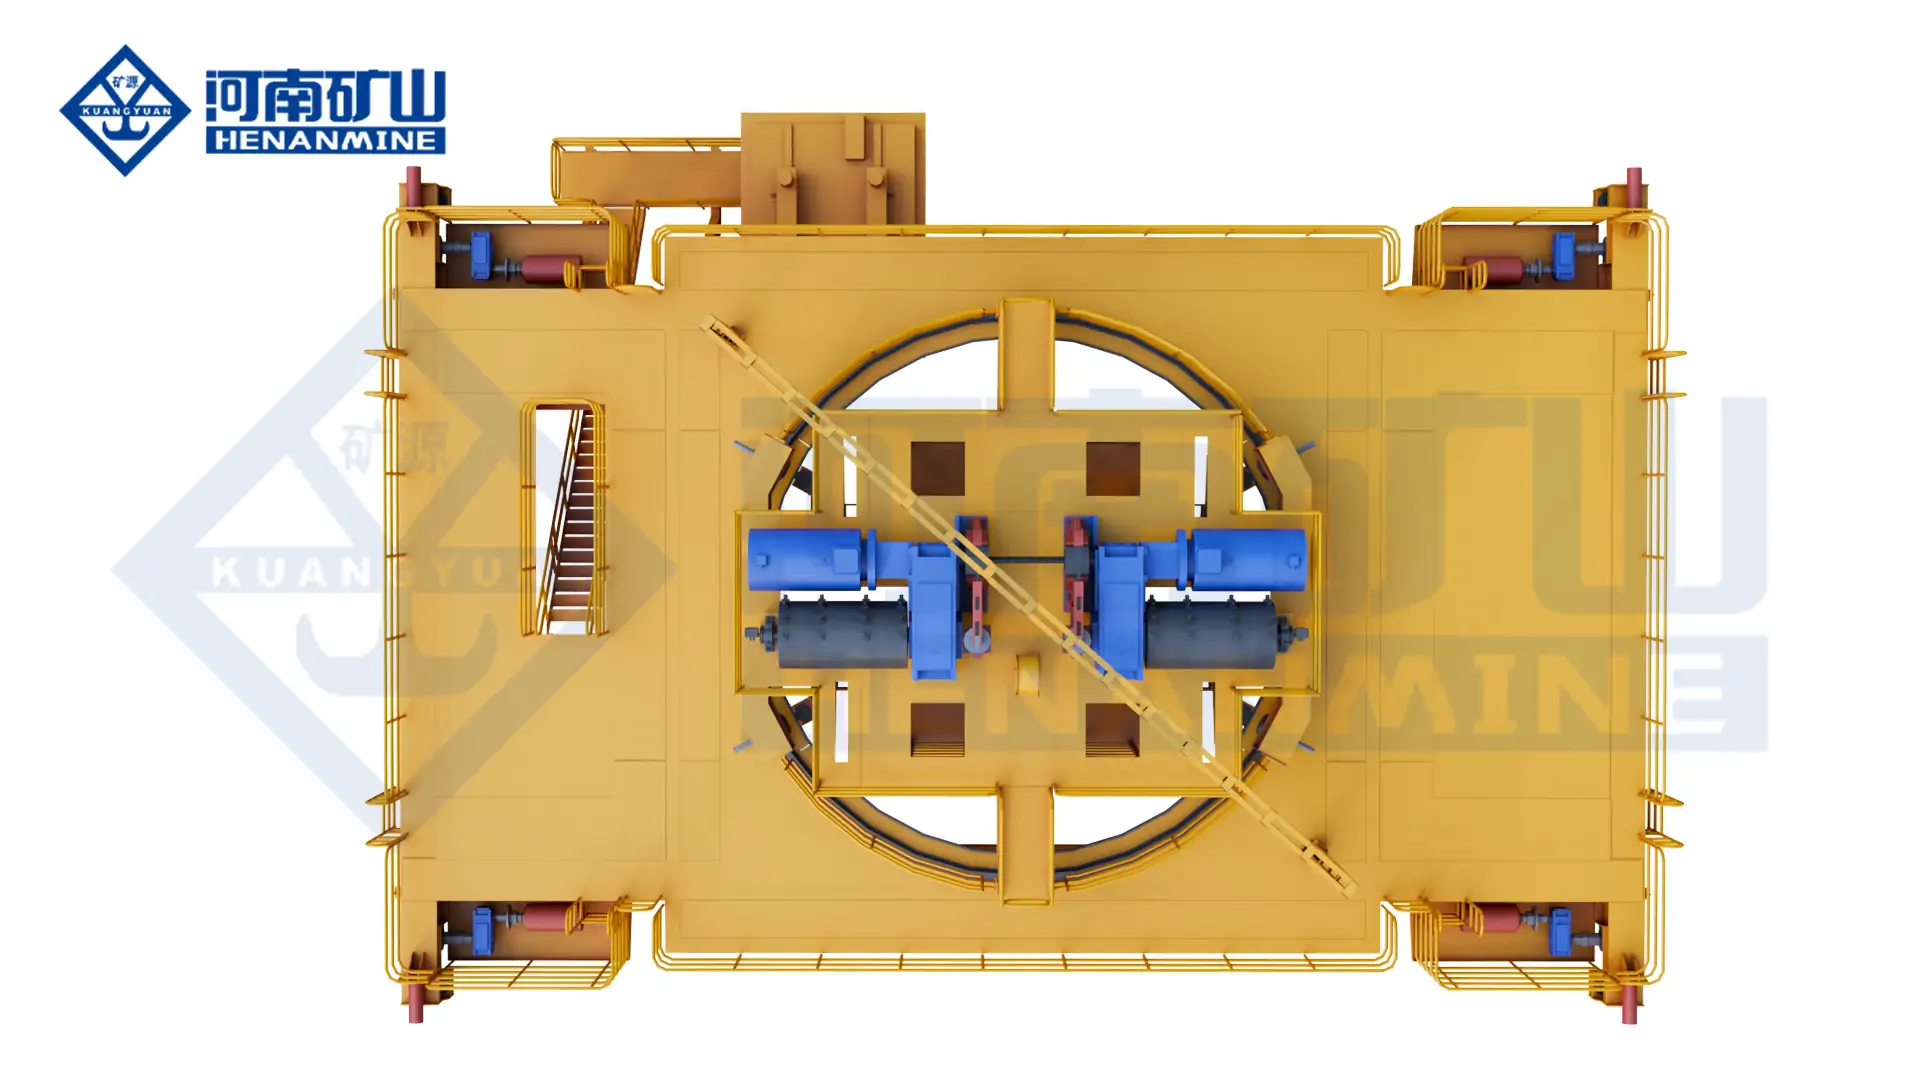
Upper-Rotating Magnetic Overhead Crane
Slewing-trolley magnetic system positioning coils and steel products at multiple angles without extra handling steps.

Double Girder Bridge Crane
Customizable overhead crane platform for C-hook, tong, beam and other engineered coil handling attachments.

Metallurgical Bridge Crane
Heavy-duty overhead crane family for demanding steel and metallurgical production, including integrated heavy coil service.
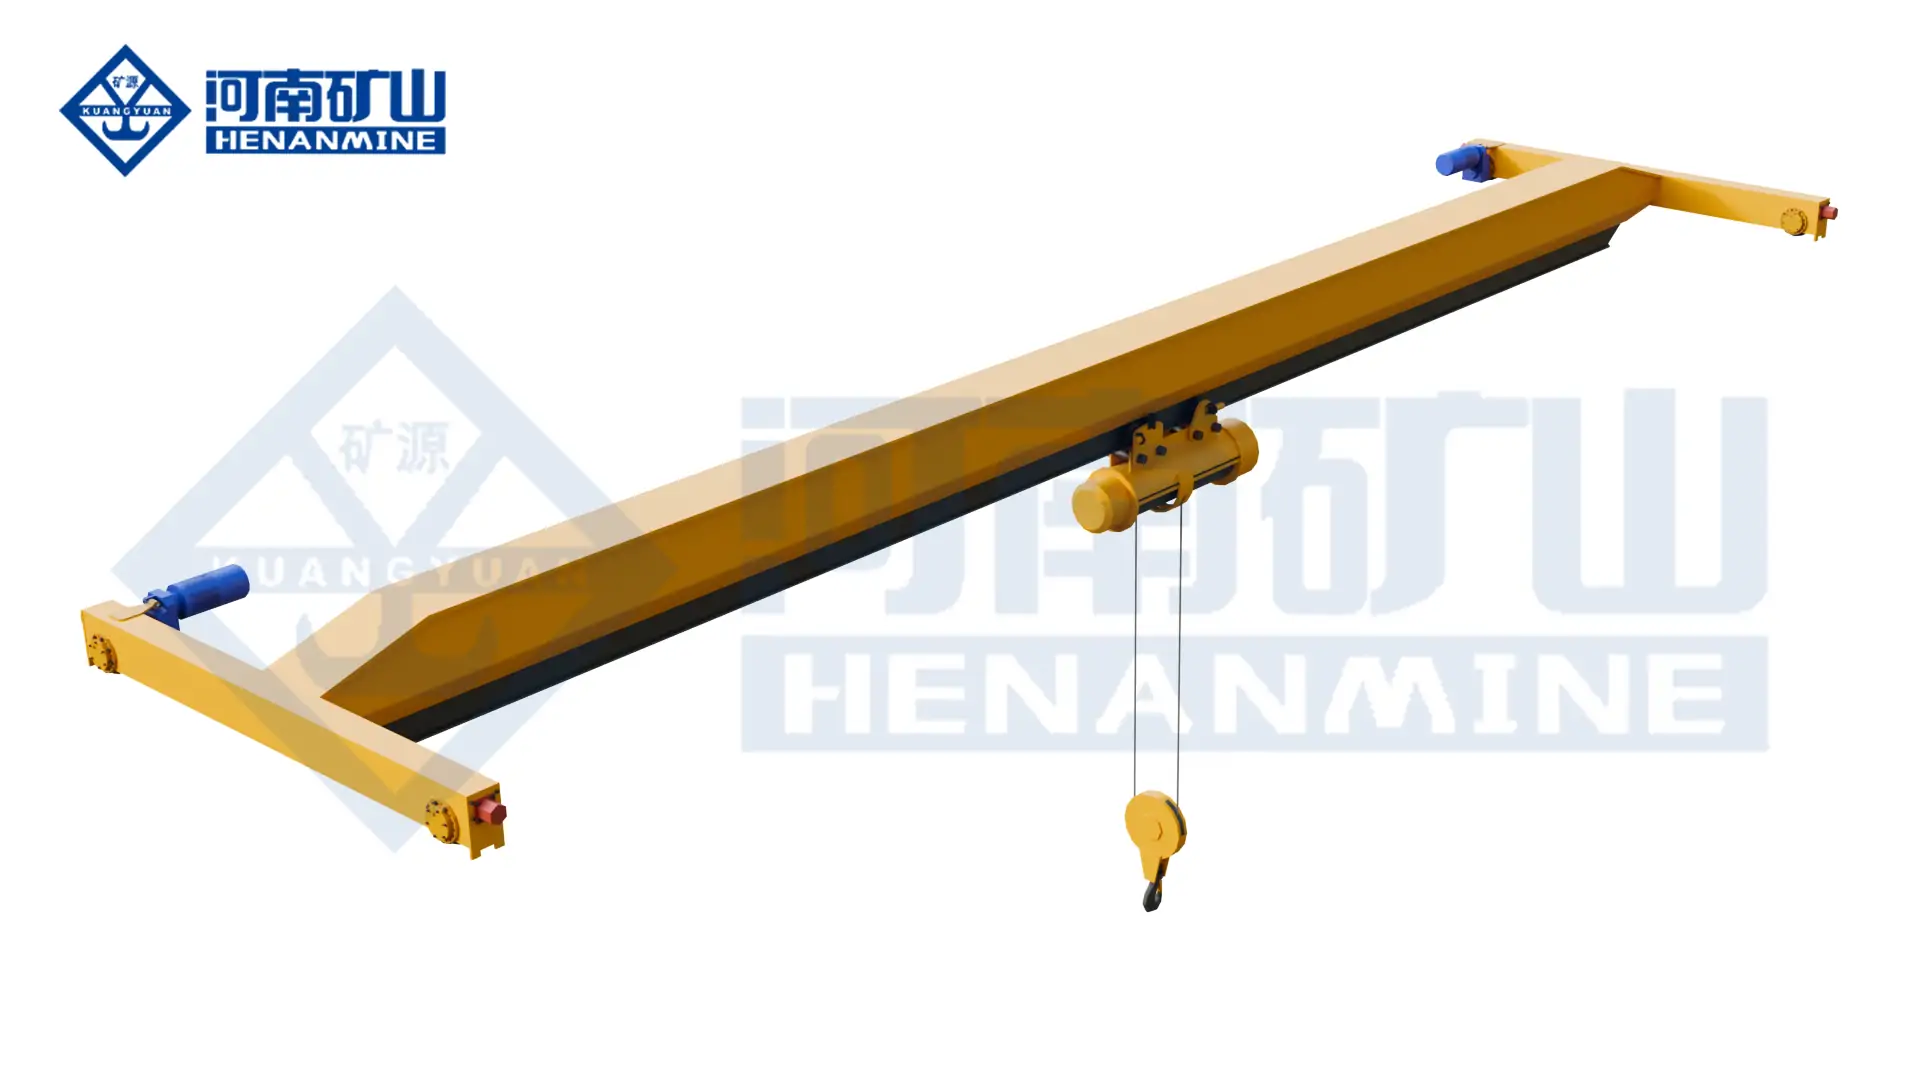
Single Girder Bridge Crane
Economical platform for light and return coils and auxiliary handling across storage and preparation areas.
Get a Coil Handling System Engineered for Your Coil Schedule
Send the coil schedule, surface classes, storage layout and cycle rate and receive a configured proposal with the crane, rated attachment, duty classification, control system, documentation and delivery schedule for your plant.