Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

博客

  • How to Purchase Multifunctional Loading Crane for Electrolytic Aluminum Plant?

    How to Purchase Multifunctional Loading Crane for Electrolytic Aluminum Plant?

    How to Purchase Multifunctional Loading Crane for Electrolytic Aluminum Plant?

    Aluminum electrolysis plant is one of the most demanding industrial scenarios. Many overseas aluminum plants and new pre-baked anode electrolysis projects are prone to step on the pitfalls in equipment procurement, because they confuse the special lifting equipment for electrolytic aluminum with ordinary workshop Overhead Cranes.

    Electrolytic aluminum multifunctional cranes, also often called PTM electrolytic aluminum multifunctional units, pole changing cranes, multi-purpose tank cranes in the industry, is the core process equipment of the pre-baked anode electrolytic aluminum production line, rather than ordinary auxiliary lifting equipment. The whole set of equipment undertakes the key process of electrolysis production, and the stability of the equipment directly determines the capacity and safety of the whole aluminum electrolysis production line.

    Unlike conventional lifting equipment, multifunctional crane for electrolytic aluminum plant needs to be adapted to the harsh environment of high temperature, strong magnetic field, hydrofluoric acid corrosion and high dust for a long time. When purchasing this kind of equipment, we should not only look at the tonnage and span, but also match the production process, environmental protection, automatic control system and long-term operation and maintenance requirements.

    Combined with many years of service global aluminum plant, EPC turnkey project hands-on experience, I put together a complete set of procurement selection logic, covering the process verification, parameter definition, functional configuration, environmental adaptation, supplier screening and other processes, to help procurement and engineering personnel to accurately select the type, to avoid the industry’s common misconceptions.

    what is a multi-function crane for electrolytic aluminum plants

    Basic definition

    Electrolytic aluminum multifunctional crane is specially designed for large pre-baked anode electrolytic aluminum production line customized special overhead cranes, but also aluminum electrolysis workshop exclusive aluminum smelter Crane, which is different from the general lifting equipment, the core positioning of the process equipment, not just for handling materials, but the depth of participation in the whole process of electrolytic production.

    Many professional names in the industry refer to the same kind of equipment, including Pot Tending Machine (PTM), Multi-Purpose Pot Crane (MPPC), Tank Work Unit, Pole Changing Unit, which are used interchangeably in the drawings and bidding documents of different oversea projects, but the core functions of the equipment are identical with the adapted scenarios.

    Core Process Functions

    A qualified electrolytic aluminum multifunctional crane can complete most of the core processes in the electrolysis plant without the need for multiple auxiliary equipment. This is the core reason why modern large-scale aluminum electrolytic workshop is generally equipped with integrated multifunctional Crane as standard.

    The regular integrated functions of the equipment include electrolysis tank crust crushing, alumina and fluorine salt dosing, old anode dismantling, new anode accurate replacement, tank slag cleaning, aluminum water package lifting and running, and anode busbar lifting and debugging. At the same time, it can cover the daily maintenance of electrolyzer, track cleaning, workshop auxiliary lifting and other supporting work.

    All operational aspects of the high concentration of carbon powder, alumina dust, asphalt fumes, hydrofluoric acid corrosive gases, high temperature molten salts and ultra-strong magnetic field under the composite environment to complete, which is the core reason why ordinary Cranes can not replace it.

    the first step: check the electrolysis production process fit requirements

    Confirmation of pre-baked anode electrolyzer parameters

    Each aluminum plant electrolysis production line parameters are not uniform, directly determines the overall design of multi-functional cranes. Pre-procurement must accurately sort out the basic data of the production line to avoid mismatch of the process and failure to put into operation after the equipment is on site.

    The basic information that needs to be focused on checking contains the capacity of a single electrolytic tank, the layout of the entire inter-tank column, the anode size and weight of a single piece, the center spacing of the tank, the width of the workshop operating channel, and the form of busbar structure. These data are the core basis for subsequent equipment spans, lifting heights, and tooling configurations.

    Defining the required integrated processes

    Different production capacity, different process positioning of the aluminum electrolysis workshop, the functional requirements of the Crane varies greatly. Some small and medium-sized aluminum plants only need basic pole changing and maintenance functions, while large intelligent aluminum plants need to integrate a full set of automated work processes.

    Before purchasing, you need to confirm one by one whether the equipment needs to be integrated with the functions of crust crushing, automatic charging, slag cleaning, aluminum water discharge, busbar lifting, and full tank overhaul. The more integrated functions, the higher the requirements for the structure of the workpiece trolley, control logic, precision and stability of the hydraulic system, but also to reserve sufficient space for later maintenance.

     the second step: the definition of the core technical parameters

    Rated lifting capacity

    Calculation of the lifting capacity of the multifunctional crane for aluminum electrolysis can not only refer to a single load weight, but also need to integrate a number of weight parameters accounting, while leaving a safety margin, suitable for long-term high-frequency operating conditions.

    The scope of calculation includes the self-weight of anode assembly parts, the full load weight of aluminum water package, the self-weight of assembly trolley and the weight of all kinds of auxiliary lifting equipment. The mainstream configurations in the industry range from 10t+10t to 40t+40t, and Henan Mine Crane can provide fully customized tonnage configurations according to the specifications of the tanks and operational requirements of overseas projects.

    Equipment Span

    The span is determined by the overall layout of the electrolysis workshop, and the core reference is the width of the workshop building, the center distance of the track, the way of arranging the tanks and the width of the maintenance access. At the same time, it is necessary to match the maximum operating range of the tooling trolley to ensure that the equipment can cover all the electrolyzer operating points.

    The conventional span of the industry ranges from 22.5 m to 34.5 m. For large-scale new aluminum plants and expansion projects overseas, larger spans can be customized to fit the site layout without changing the plant structure.

    Lifting height

    The core of the design of lifting height is to avoid obstacles in the workshop and ensure safe operation under all working conditions. It is necessary to reserve sufficient clearance for anode lifting and lowering, aluminum water package lifting height, busbar operation height, and maintenance operation space above the electrolytic tank.

    At the same time, it is necessary to accurately calculate the limit approach distance of the hook, so as to avoid collision with the tank, pipeline and workshop structure when lifting anode and aluminum water package, and to eliminate the risk of equipment interference.

    Working level

    Different from ordinary auxiliary cranes, aluminum electrolysis crane belongs to continuous operation process equipment, the working level must match the intensity of production line operation, and can not be applied to general equipment standards.

    When selecting a crane, it is necessary to make a comprehensive judgment based on the daily operating hours of the tank column, the number of electrolysis cells to be served, the frequency of single-process operation, the cycle of production and the maintenance load. For large-scale mass production aluminum electrolysis workshop, it is necessary to choose high working level configuration, which is suitable for uninterrupted high-frequency operation throughout the year and reduces the probability of failure and downtime.

    Multifunctional Suction Crane for Aluminum Electrolysis

     Selection of core functional modules

    Tooling trolley

    Tooling trolley is the core operating unit of the electrolytic aluminum multifunctional Crane, which directly determines the equipment’s ability to work on the process, and is also the core component that distinguishes it from ordinary cranes.

    The complete tooling system can integrate the crust crushing mechanism, automatic pole changing mechanism, slag cleaning mechanism, material dosing and feeding mechanism, 360-degree rotating mechanism and cab rotating mechanism. The whole set of structure and hydraulic system work together to complete all electrolysis process operations.

    Aluminum Lifting Trolley

    The trolley module is specially used for the transfer of aluminum water ladle and aluminum discharge operation, which is the necessary configuration for mass production aluminum plants. The selection focuses on the rated lifting tonnage, weighing accuracy, suitability for vacuum aluminum discharge, and the design of an exclusive safe transport path.

    Meanwhile, the structure of the trolley should be equipped with a heat-insulating protection design to resist the high-temperature radiation of aluminum water, avoid the aging and deformation of components caused by long-term high-temperature operation, and ensure the stable operation of the aluminum discharge process.

    Material Charging System

    The dosing system is mainly responsible for the accurate supply of electrolysis raw materials such as alumina and fluorine salt. When purchasing, it is necessary to confirm the dosing method, material particle size suitability, dust control program and automatic/manual switching mode.

    High quality dosing system can realize quantitative and uniform feeding, reduce the waste of raw materials, and at the same time, it is equipped with sealing and dust-proof structure to reduce the concentration of dust in the workshop, which is suitable for the harsh production environment.

    Automatic pole changing system

    Pole changing is the most frequent core process in the electrolysis workshop, and the automatic pole changing system can greatly reduce manual intervention and improve operational precision. The equipment should be equipped with the functions of automatic loosening and tightening of clamps, smooth lifting of old anodes, precise installation of new anodes, and auxiliary functions of cleaning residual electrodes.

    Stable pole changing system can effectively reduce the error of manual operation, avoid the deviation of anode installation affecting the production condition of electrolyzer, and ensure the smooth operation of the production line.

    Adaptation to the design of protection against harsh working conditions in aluminum plant

    Adaptation to high-temperature environment

    The operation area of the electrolyzer is in high temperature for a long time, and the ambient temperature around the tank is much higher than that of a common industrial workshop, and there is also high temperature heat radiation from molten salt. Ordinary lifting equipment cables, hydraulic piping, electrical components, will be quickly aging and failure.

    Specialized crane for aluminum smelting plant will use high-temperature resistant cables, insulated electrical cabinets, protective hydraulic piping layout, all components near the high-temperature area are heat-insulated and flame retardant treatment, suitable for long-term high-temperature operating scenarios.

    Strong magnetic field anti-interference design

    Aluminum electrolysis production relies on high-current DC operation, the workshop will form a strong and stable magnetic field, which will seriously interfere with sensors, weighing systems, PLC control modules and precision electrical components, resulting in positioning deviations and data distortion.

    Professional aluminum multifunctional cranes will do a full set of anti-magnetic design, electrical cabinets, control systems, testing components to do shielding protection, from the root to avoid magnetic interference, to protect the positioning accuracy and stability of equipment operation.

    HF corrosion and dust protection

    Hydrofluoric acid corrosive gas, fluorine salt particles, alumina dust, carbon powder and asphalt fumes are the main causes of aging and failure of aluminum workshop equipment. Dust buildup can clog drive structures, and corrosive gases can eat away at steel structures and electrical connections.

    Standard protective configurations include fully sealed electrical cabinets, specialized heavy-duty anticorrosive coatings, dust-proof enclosed drive components and anticorrosive cable systems to provide all-round protection against corrosion and dust, and extend the service life of the equipment.

    the fifth step: confirm the automation and control system configuration

    PLC integrated control system

    The whole set of multifunctional Crane bridge operation, trolley walking, workpiece operation, charging, pole changing, aluminum output and all other processes, need to rely on PLC control system collaborative linkage.

    Integrated PLC control can realize the synchronous and coordinated operation of each mechanism, avoid action conflicts caused by individual operation, and guarantee the orderly landing of complex processes, which is the standard for multifunctional cranes in modern aluminum factories.

    Variable frequency speed control (VFD)

    VFD frequency conversion control can realize smooth starting and stopping of equipment, and alleviate load shaking and mechanical impact during operation. In high-precision operation scenarios such as pole changing, aluminum output and busbar lifting, it can accurately control the operation speed and enhance the stability of operation.

    This configuration can effectively reduce the mechanical wear and tear of the equipment, lower the cost of operation and maintenance in the later stage, and is suitable for high-frequency and continuous production operations.

    Matching of control modes

    The mainstream control mode suitable for aluminum plant working conditions is the rotating cab + wireless remote control dual mode. The cab can meet the normalization and refinement of the operation, and the remote control can keep the operator away from the high temperature, corrosion, strong magnetic high-risk work area, to enhance the safety of the operation.

    The equipment is also equipped with emergency manual operation mode, which can be used manually when the automatic control system fails to avoid the whole production line shutdown.

    Data recording and weighing function

    High-end configuration includes weighing of aluminum water package, weighing of single batch materials, cumulative data statistics, data export and production data linkage functions. These data can be connected to the factory production management system to facilitate production capacity statistics, material accounting and production traceability, which is suitable for the management needs of modern intelligent aluminum factories.
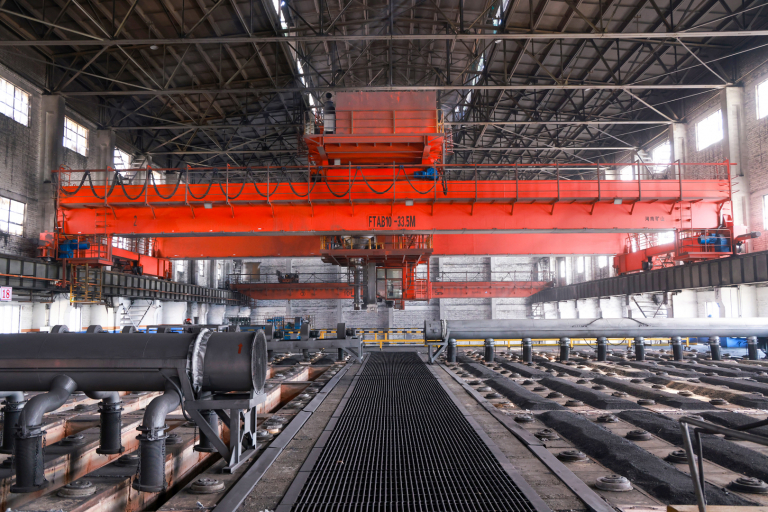
    Multifunctional Suction Crane for Aluminum Electrolysis

    step six: verify the exclusive safety configuration

    Aluminum electrolysis Crane belongs to high-risk process equipment, the safety configuration can not follow the standard of ordinary vehicles, must be adapted to the special working conditions of the aluminum plant, all-round avoidance of operational risks.

    Overload protection device

    When changing poles, lifting aluminum water packages, tank maintenance and other heavy-duty operations, the overload protection device can monitor the load in real time, and automatically lock the lifting action when it exceeds the rated tonnage, so as to eliminate the risk of damage to the equipment and fall of materials caused by overloaded lifting.

    Multiple Limit Protection

    The equipment is equipped with upper and lower lifting limits, trolley traveling limits, trolley running limits, and slewing mechanism limits, which all-roundly restrict the equipment running boundaries, avoiding over-traveling and collision with workshop frames, troughs and pipelines.

    Anti-collision system

    Large electrolysis workshop will be arranged within the same span of more than one lifting equipment, anti-collision system can be real-time monitoring of equipment spacing, automatic warning, deceleration, shutdown, to avoid collision accidents occurring in the cross operation of multiple equipment.

    Emergency stop system

    Emergency stop button covers the driver’s cab, remote control terminal, electrical cabinet, maintenance platform at multiple points, when a sudden failure can be cut off at any time, anywhere, the power supply of the equipment, rapid shutdown to avoid danger.

    Fire insulation and hydraulic protection

    The high temperature area adopts flame retardant cables, heat insulated cabinet and fireproof piping layout. The hydraulic system is equipped with pressure protection, anti-leakage structure, and emergency reset function, while reserving sufficient space for maintenance to avoid safety hazards caused by hydraulic leakage.
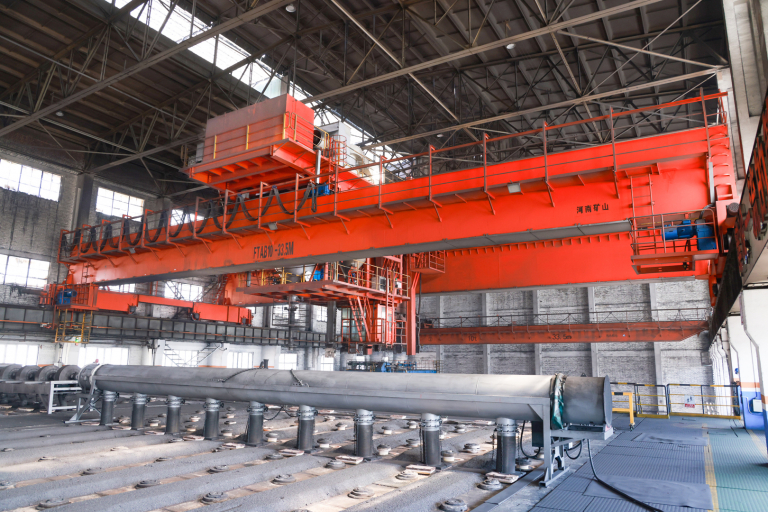
    Multifunctional Suction Crane for Aluminum Electrolysis

    Verification of structural design and track adaptation

    Main bridge structure

    Aluminum electrolysis multifunctional Crane adopts box-type double or triple girder reinforced structure, with reinforced rail and high-strength steel, adapted to heavy-duty, high-frequency, bumpy operating conditions. The overall structure is more rigid, not easy to deform, and can withstand the wear and tear of harsh environments for a long time.

    Wheel Pressure and Track Adaptation

    Suppliers are required to provide accurate maximum wheel pressure parameters, suitable track model, track foundation interface data and end beam layout program. Wheel pressure data is the core basis for structural checking of the plant. Many overseas projects fail to check the wheel pressure in the early stage, resulting in the plant not being able to carry the equipment, and the cost of reworking and rectification is extremely high.

    Design of maintenance access

    Considering the harsh environment of high corrosion and dust in the aluminum plant, the equipment must be reserved for standardized maintenance platforms, safety ladders, access ports for tooling trolleys, electrical cabinets, and hydraulic system operation space, which is convenient for daily inspection, maintenance, and replacement of spare parts, and reduces the difficulty of operation and maintenance in the later stage.

    step eight: supplier strength assessment checklist

    Aluminum electrolysis multifunctional crane belongs to the customized high-end process equipment, equipment quality, adaptability, after-sales protection is completely dependent on the supplier’s industry accumulation, ordinary general-purpose crane manufacturers can not meet the demand.

    Aluminum plant project hands-on experience

    Priority is given to suppliers with experience in pre-baked anode aluminum plants, PTM units in electrolysis shops, and automated pole-changing Crane projects. Focus on verifying overseas aluminum plant cases, experience in supporting equipment for the entire tank column, and confirming that the manufacturer is familiar with the process standards and compliance requirements of international projects.

    Professional engineering capability

    Reliable suppliers can provide complete process adaptation solutions, tooling structure diagrams, workshop layout matching diagrams, wheel pressure calculations, electrical control logic and hydraulic system design instructions, and can optimize customized solutions according to on-site working conditions instead of applying standard models.

    Production and Testing Capability

    We need to have the ability of large-scale steel finishing, complete machine assembly, PLC and hydraulic system integration and debugging, and complete a full set of load test, electrical test and hydraulic pressure test before leaving the factory, so as to ensure that the equipment meets the standard and reduce the on-site debugging failures.

    Full process after-sales support

    Overseas projects focus on spare parts supply, remote troubleshooting, on-site commissioning guidance, operator training and regular maintenance guidance. One day of equipment downtime in aluminum plant will cause huge capacity loss, and a perfect after-sales system is the guarantee for long-term stable production.
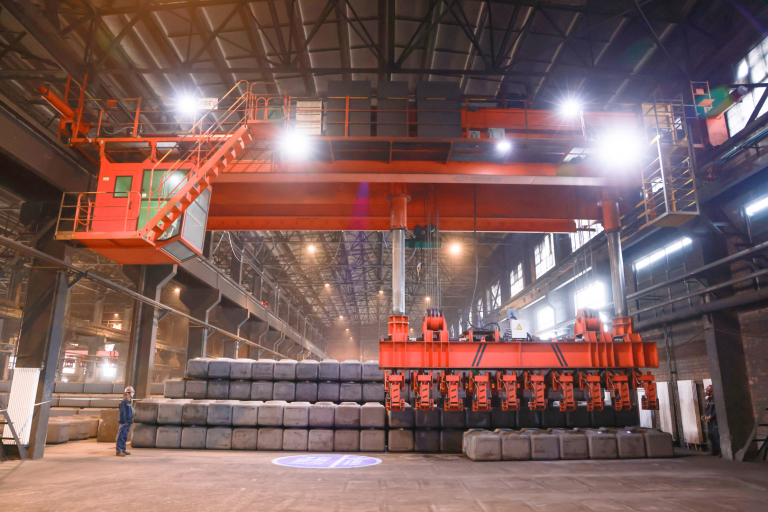
    Anode Charcoal Block Stacking Crane for Aluminum Electrolysis

    the ninth step: procurement of essential documents verification

    Overseas project acceptance, customs clearance, production verification, all need a complete set of documents, procurement must clearly require suppliers to provide all.

    Technical documents

    Containing equipment assembly diagrams, workshop layout matching diagrams, tooling structure diagrams, wheel press drawings, electrical schematic diagrams, hydraulic schematic diagrams, PLC control instructions, safety configuration lists and complete technical parameter tables.

    Business documents

    Contain quotation details, delivery period, installation and commissioning scope, spare parts list, warranty terms, training content and payment method description.

    Acceptance documents

    Contain factory test report, load test record, electrical test report, hydraulic system test report, weld flaw detection report, anti-corrosion coating test report, equipment operation and maintenance manual, spare parts catalog.
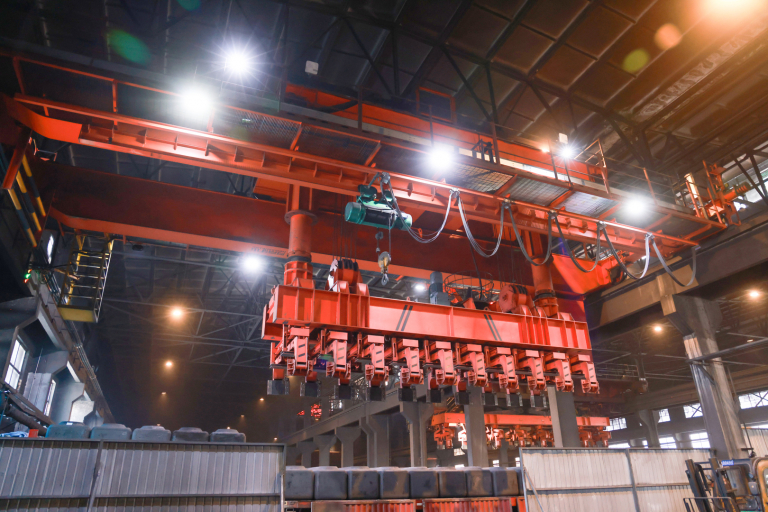
    Anode Charcoal Block Stacking Crane for Aluminum Electrolysis

     Full Life Cycle Costing

    Front-end input (CAPEX)

    In addition to the main structure of the equipment, it also contains a full set of pre-inputs, such as tooling trolley, aluminum system, charging equipment, hydraulic unit, automatic control system, on-site installation and debugging, etc. When purchasing, it is necessary to account for the overall cost of the complete set, not a single equipment offer.

    Post-operation and maintenance costs (OPEX)

    Long-term operation and maintenance includes the replacement of hydraulic parts, replacement of electrical wear parts, wheel track maintenance, replacement of wear parts of work equipment, spare parts inventory reserves and other costs. High-quality equipment has a high investment in the early stage, but the failure rate in the later stage is low, and the operation and maintenance cost is more controllable.

    Downtime risk cost

    Crane is the core equipment of the production line, once the failure of the production line stops, it will directly lead to the stagnation of the pole changing, charging, and aluminum process, and the whole production line will be reduced or even shut down. Selection of priority consideration of equipment reliability and maintainability, far more important than the low price.

    Anode Charcoal Block Stacking Crane for Aluminum Electrolysis

    aluminum plant multifunctional crane procurement common misunderstandings

    A lot of procurement mistakes, are derived from the cognitive bias of the equipment attributes and working conditions. The most common mistake is to equate the process-type multifunctional Crane with ordinary Overhead Crane, according to the general equipment standard selection and procurement, and ultimately the equipment can not be adapted to the production conditions.

    Neglect of HF corrosion, strong magnetic interference, high temperature protection and other special design requirements, is a high frequency of overseas projects to step on the pit. Lack of anti-magnetic, anti-corrosion, high-temperature resistant configuration of the equipment, put into operation within a short period of time will be electrical failures, structural corrosion, positioning inaccuracy and other problems.

    In addition, screening suppliers only by price, not specifying the functional list of tooling, not checking the wheel pressure data, ignoring the convenience of hydraulic system maintenance, and not planning the spare parts reserve in advance will lead to project delays and soaring operation and maintenance costs.
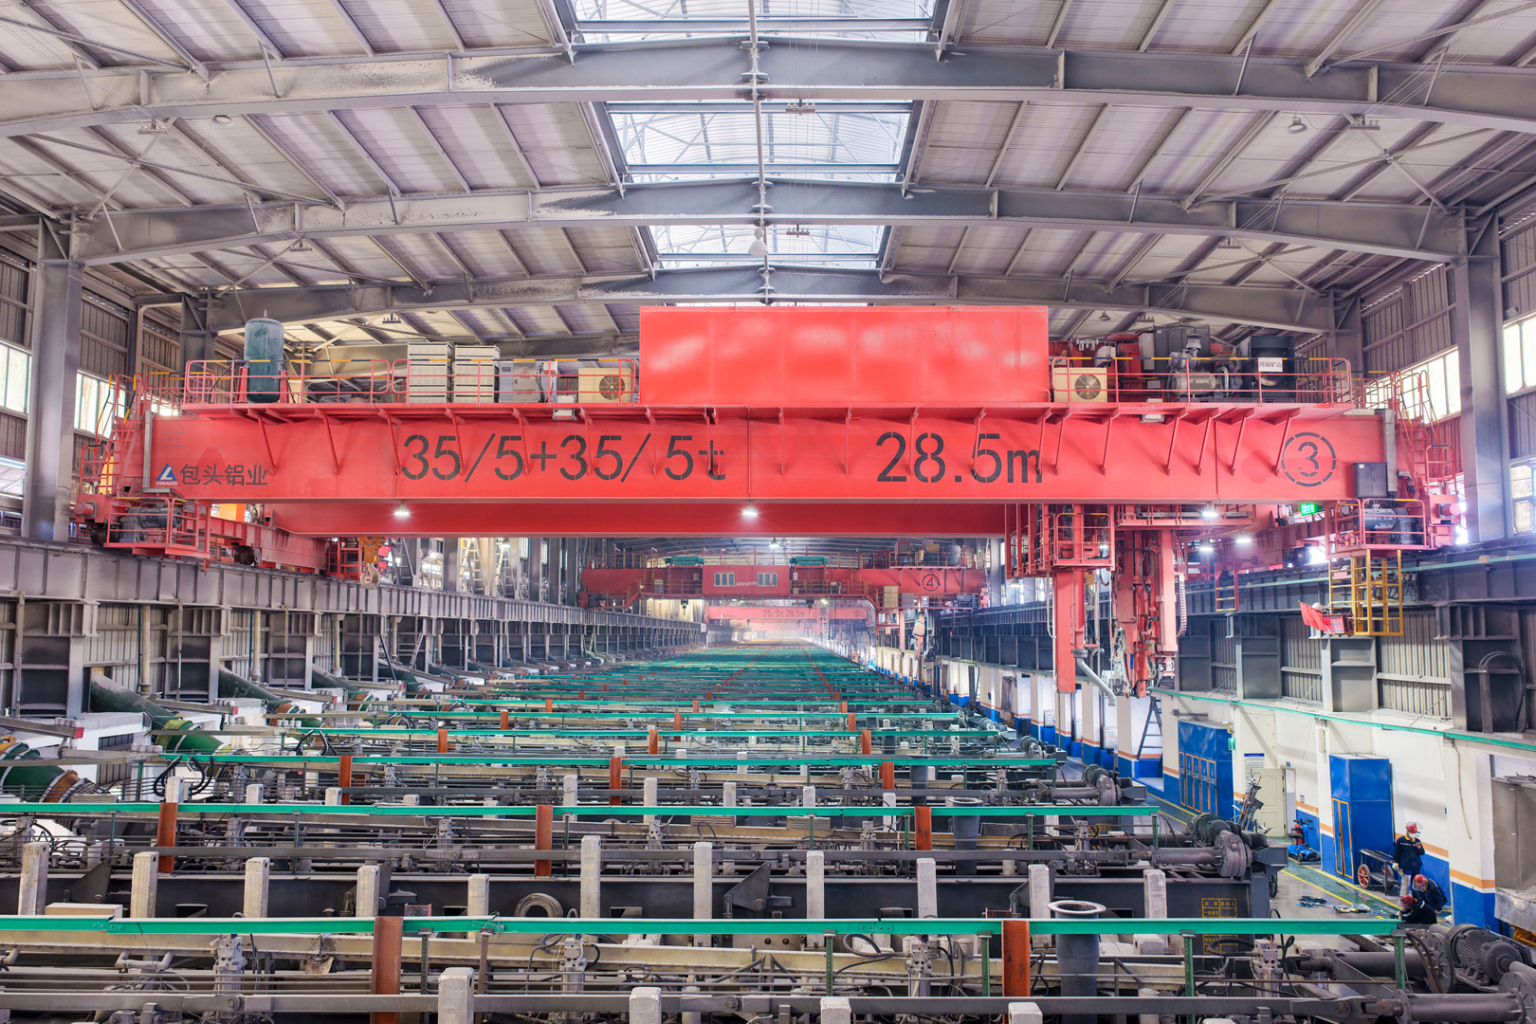
    Anode Charcoal Block Stacking Crane for Aluminum Electrolysis

    procurement RFQ quotation preparation list

    Before launching RFQ to suppliers, organize complete information in advance, which can greatly improve the accuracy of the program and avoid repeated communication and rewriting. The core information to be prepared is as follows:

    Workshop tank layout drawings, electrolytic tank model specifications, the number of service tanks, anode size and weight, residual electrode processing requirements, aluminum water package rated capacity, equipment span, lifting height, track gauge, site operating temperature, corrosion and dust conditions, power supply parameters, control modes, automation level, tooling functional requirements, certification standards, installation and commissioning requirements.

    Frequently Asked Questions FAQ

    What is the core difference between electrolytic aluminum multi-function crane and ordinary traveling crane?

    Ordinary traveling crane is only used for simple material lifting, belonging to auxiliary equipment. Aluminum electrolysis multifunctional Crane is an integrated process equipment, which integrates a full set of production processes, such as pole changing, crust crushing, charging, aluminum discharge, slag clearing, maintenance, etc. Meanwhile, it is equipped with special protection capabilities of high temperature resistance, anti-magnetic and corrosion resistance, which is suitable for the extreme working conditions of the aluminum plant.

    Are the PTM unit and the Aluminum Multi-function Crane the same equipment?

    Yes, they are. In the global aluminum electrolysis industry projects, Pot Tending Machine (PTM), MPPC multi-purpose tank crane, electrolytic aluminum multi-purpose cranes all refer to the same type of special equipment, only the industry called different.

    Is tonnage the most important parameter for selection?

    No. Tonnage is only the basic parameter. Tonnage is only a basic parameter, the real decision of whether the equipment can be put into operation is the ability to adapt to the process. Including pole changing, charging, aluminum and other functional matching, as well as anti-magnetic, anti-corrosion, high temperature protection design, which is the core attributes of general-purpose cranes do not have.

    Why anti-corrosion, anti-magnetic design is essential?

    Hydrofluoric acid gas, fluorine salt dust, strong magnetic field in aluminum electrolysis workshop will continue to erode the steel structure, interfere with the electrical system, loss of precision components. Equipment that lacks special protection has an extremely high failure rate and a greatly shortened service life, making it impossible to ensure continuous production.

    Do I have to use PLC and VFD control systems?

    This is basically standard in modern aluminum plants. The whole set of equipment and multiple organizations work together, need PLC to realize the logic of linkage, VFD frequency conversion to ensure smooth and accurate operation, not only to improve production efficiency, but also to reduce equipment loss and safety risks.
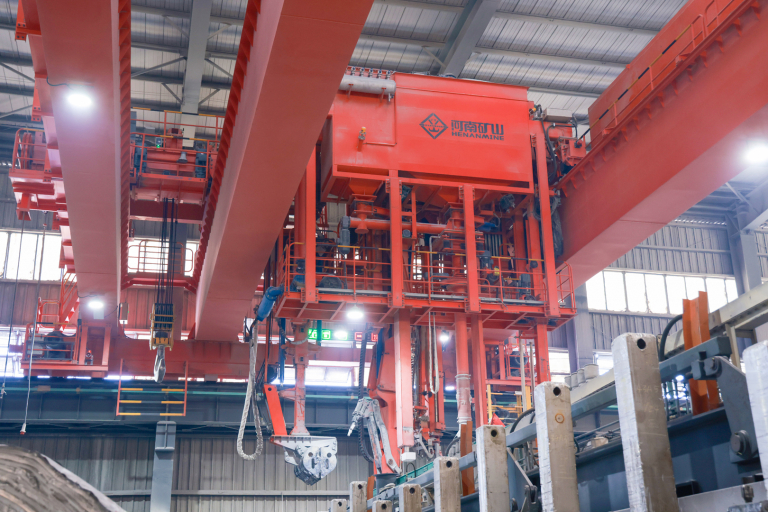
    Multifunctional Unit for Aluminum Electrolysis

    Henan Mine Crane Factory Custom

    Procurement of multifunctional crane for electrolytic aluminum plant, the essence is to choose a set of core process solutions to adapt to the aluminum electrolysis production line, rather than simply purchasing a lifting equipment.

    A quality multifunctional Crane for electrolytic aluminum plant needs to fully match the tank layout, electrolysis process, extreme working conditions and automated production requirements, while providing stable performance and convenient operation and maintenance conditions. Highly adaptable equipment can effectively simplify the workshop workflow, reduce labor costs, and ensure the long-term stability of the production line and mass production.

    Henan Mine Crane, as a crane supplier, we have been plowing into the global aluminum industry for many years, with a wealth of experience in customization and landing of PTM cranes and aluminum multifunctional units, and are familiar with the standards of aluminum plants in various countries and project acceptance requirements.

    According to the customer’s site parameters, we can provide one-on-one customized solutions, a full set of technical documents and perfect overseas after-sales support to avoid the risk of selection and commissioning.

    If you need accurate equipment selection, parameter checking and project quotation, please feel free to provide the workshop working condition data, and we will provide you with professional customized solutions.
    Henan Mine CraneDiscuss your requirements ↗
  • How to Protect Port Cranes from Saltwater Corrosion

    How to Protect Port Cranes from Saltwater Corrosion

    How to Protect Port Cranes from Saltwater Corrosion

    Port cranes are exposed to harsh marine working conditions with high salt spray, high humidity, and seawater splashing for a long time. Chloride ions can easily cause metal electrochemical corrosion, and their corrosion rate is 3 to 5 times that of ordinary industrial environments.Corrosion will cause the coating of the equipment to fall off and the parts to become stuck. In severe cases, it will also lead to cracking of the steel structure, electrical short circuit, and hydraulic leakage, which will greatly increase the maintenance cost of the equipment and shorten the service life of the equipment, which directly affects the stability and operational efficiency of the port.Seawater anticorrosion is not a simple rust removal and painting, but a system engineering that runs through the whole life cycle of equipment components, design, coating, and operation and maintenance.

    Which Port Crane Components Are Most Vulnerable to Corrosion

    Not all components of port cranes have the same corrosion risk. The degree to which components of different structures, materials, and operating modes are eroded by seawater salt spray varies greatly.Accurate identification of highly corrosive and fragile parts is a prerequisite for targeted anti-corrosion protection and elimination of invalid operation and maintenance.The following six core components are areas with high incidence of seawater corrosion, and they are also the key objects of anti-corrosion control of port cranes.

    Steel structures

    The steel structure is the main load-bearing frame of the Henan Mine Crane manufactured port crane, including the main beam, end beam, gantry, tower body, walking bracket, etc., and it is also the core component with the largest exposure to salt spray and the most serious corrosion impact.In the marine environment, steel structures made of ordinary carbon steel can easily absorb salt-containing moisture on the surface, forming an electrochemical corrosion circuit.Especially in welds, edges and corners, and stress-concentrated areas, the coating can easily crack and peel. Chloride ions will continue to penetrate into the interior of the substrate, causing dot-like corrosion and layered peeling. Long-term corrosion will lead to thinning of the wall thickness of the steel structure and a decrease in carrying capacity, which directly threatens the structural safety of the crane.At the same time, poorly ventilated areas such as the bottom of the steel structure and the shady dead corners are prone to condensation and salt accumulation, and the corrosion rate is much higher than that of the exposed surface of the equipment. It is the hardest-hit area of corrosion that can be easily missed during daily inspections.

    Mechanical parts

    Mechanical moving parts are the core execution unit of crane operations, including reels, pulleys, gears, bearings, brake components, walking wheels, etc. Such parts are in dynamic friction and vibration conditions for a long time, and corrosion hazards are extremely hidden and destructive.Salt spray is attached to the mechanical fit gap, which will destroy the surface smoothness of the parts, cause slight corrosion and increased wear, and cause equipment operation to stall, abnormal noise, and brake failure.Once bearings, gears and other precision transmission components are corroded, the gap will become larger and the accuracy will be offset, which not only reduces the operating stability, but also causes overload failure and component stagnation, greatly increasing the probability of downtime and maintenance.Moreover, corrosion of mechanical parts mostly occurs inside the equipment, which is difficult to visually detect with the naked eye, and it is often only discovered after failure, and the maintenance cost is extremely high.

    Electrical systems

    The electrical system is the core control unit of Henan Mine Crane manufactured port crane, covering precision components such as control cabinets, cables, terminal blocks, sensors, limit switches, and motors, which are extremely sensitive to seawater salt spray corrosion.The high humidity and salt-containing air in the port will invade the interior of electrical equipment and form a salt film on the surface of circuit boards and wiring contacts, causing problems such as aging of the insulating layer, leakage, short circuit, and poor contact.Minor corrosion can cause abnormal signal transmission and equipment start-stop failure. In severe cases, it will cause motor burning, electrical fire, power failure and shutdown of the whole machine, causing port operations to be interrupted.Compared with mechanical corrosion, electrical system corrosion has no obvious appearance signs and is extremely sudden, which is a major invisible hidden danger in the safe operation of port cranes.

    Hydraulic components

    The hydraulic system is responsible for the core actions of crane lifting, luffing, expansion and contraction, including hydraulic cylinders, oil pumps, oil pipes, hydraulic valves, seals and other components, which are prone to corrosion and failure when exposed to salt spray for a long time.The piston rod of the hydraulic cylinder is a high-precision polished metal surface. Salt spray erosion will cause surface rust and pitting, which directly destroys the sealing of the seal, causing hydraulic oil leakage, insufficient pressure, weak lifting and other failures.At the same time, the metal corrosion of the hydraulic valve body and pipeline joints will produce rust impurities, which will be mixed into the hydraulic oil, causing blockage of the oil circuit and wear of components, accelerating the aging of the entire hydraulic system, greatly shortening the service life of hydraulic equipment, and frequently causing lifting operation failures.

    Corrosion Protection Design for Port Cranes

    Source design is the core key of seawater anticorrosion of port cranes. High-quality anticorrosive structure design can fundamentally reduce the cause of corrosion and reduce the pressure of late operation and maintenance.Unlike ordinary industrial cranes, port cranes need to make special anti-corrosion designs from the dimensions of material, structure, sealing, and drainage for high-corrosion marine conditions, so as to avoid core problems such as salt spray, stagnant water, and crevice corrosion in advance, and realize the upgrade from passive anti-corrosion to active anti-corrosion.

    Material selection

    The corrosion resistance of materials is the basis of anticorrosion. The choice of materials adapted to marine working conditions can reduce the probability of corrosion from the root cause and greatly improve the long-term protection ability of equipment.In view of the differences in working conditions of different components in the port, precise material selection is required. Marine weather-resistant steel and low-alloy anticorrosive steel are preferred for the main steel structure. The substrate has the ability to resist chloride ion erosion and is suitable for long-term salt spray exposure. Environment.Precision mechanical parts, fasteners, and pins are made of ordinary carbon steel, and stainless steel and alloy anticorrosive materials are used to improve the dual properties of wear resistance and corrosion resistance.The electrical shell and hydraulic joints are made of anticorrosive aluminum alloy and modified plastic materials to avoid electrochemical metal corrosion.The seals and oil pipes are made of fluorine rubber and polyurethane materials that are resistant to salt spray and aging to prevent corrosion, aging and failure.Scientific material classification and selection can directly reduce the risk of native corrosion by more than 60%.

    Sealed components

    Sealing design is the core means to block salt spray and seawater from invading the interior of the equipment, focusing on the electrical system, hydraulic system, and precision moving parts to do full sealing protection.All electrical control cabinets, junction boxes, and motor end caps are made of waterproof and dustproof sealing tape, with a closed structure design to prevent salt spray and moisture from invading the interior.The hydraulic cylinder and hydraulic valve body adopt a combined sealing structure, and a dust-proof protective sleeve is added to the outside to isolate the attachment of seawater splashing and salt spray.Precision transmission components such as bearings and gears are designed with a closed box, filled with long-lasting anticorrosive grease, and the corrosive medium is blocked from contacting the metal substrate.At the same time, all equipment interfaces, cable perforations, and pipeline joints are sealed and blocked to completely cut off the penetration channel of corrosive media and protect the safety of internal precision components.

    Drainage design

    Stagnant water and salt accumulation are the core inducement to accelerate the corrosion of port equipment. Static saline stagnant water will continue to cause electrochemical corrosion of metals, so scientific drainage structure design is essential.Henan Mine Crane manufactured crane steel structure box, main beam, end beam, base and other closed cavities, standardized drainage holes and ventilation holes need to be reserved to prevent the accumulation of rainwater, seawater, and condensate.The equipment platform, walking bracket, and flange contact surface are designed with an inclined diversion structure to ensure that the stagnant water is quickly discharged from the flow and there is no residual dead angle.A diversion channel is added to the water-prone area at the bottom to avoid long-term attachment of salt spray condensate.At the same time, the drainage holes are designed to be anti-clogging to prevent debris and rust residues from clogging the drainage channels, ensure unobstructed drainage around the clock, and reduce the problem of stagnant water corrosion from the root cause.

    Crevice reduction

    Crevice corrosion is the most common type of concealed corrosion in port cranes. Component splicing gaps, welding gaps, and connection gaps can easily accumulate salt dust and water, forming a local highly corrosive environment, and the internal ventilation of the gaps is poor, difficult to clean, and the corrosion rate is much higher than that of the exposed surface.In the equipment design stage, it is necessary to minimize structural gaps. The full welding process is used for steel structure splicing to replace spot welding and lap welding, and the welds are polished and smoothed to eliminate welding gaps.The connection of the components adopts an integral structure to reduce the splicing points.After the bolts and pins are installed, they are blocked and wrapped to eliminate the connection gap.All edges, corners and splicing gaps should be rounded and polished to avoid salt and water accumulation in the stress gaps, and reduce the risk of crevice corrosion in all directions.

    Choosing the Right Anti-Corrosion Coating System

    Anticorrosive coating is the core and most commonly used external protective barrier for port cranes. The high-quality multi-layer coating system can form a dense protective film on the surface of the metal substrate to isolate the erosion of chloride ions, moisture, and oxygen.Under the high corrosion conditions of port C5-M, ordinary single-layer coatings cannot meet the long-term protection needs at all. A multi-layer professional anticorrosive coating system of surface pretreatment, primer, middle paint, and top paint must be used for layer-by-layer construction, with standardized construction and testing technology to achieve long-term anticorrosive effects.

    port crane corrosion protection

    Surface preparation

    The surface treatment of the substrate is the basis for the protective effect of the coating. Data show that more than 80% of the coating shedding and anticorrosive failure problems are due to substandard surface treatment.Before the coating construction of Henan Mine Crane manufactured port crane, the substrate must be pretreated to a high standard. First, the rust, oxide skin, old coating, oil, salt and dust impurities on the surface of the steel must be completely removed by sandblasting and shot blasting. The cleanliness of the substrate must reach the Sa2.5 level standard, and the surface forms a uniform rough surface to enhance the adhesion of the coating.For key areas such as welds, dead corners, edges and corners, manual polishing and refinement are used to eliminate residual impurities.The treated substrate needs to be primed and coated within 4 hours to avoid secondary oxidation and salt accumulation, ensure that the coating is closely integrated with the substrate, and eliminate the problem of stratification and shedding.

    Zinc-rich primer

    Epoxy zinc-rich primer is the core underlying protection of the port’s anticorrosive coating system. It mainly has the function of cathodic protection and is the first line of defense for anticorrosive steel structures.The primer contains a high content of zinc powder, the zinc metal activity is higher than that of steel, and the oxidation reaction can occur first, sacrificing itself to protect the steel substrate from corrosion, while forming a dense protective layer to block the penetration of corrosive media.Under high corrosion conditions in ports, special marine epoxy zinc-rich primers need to be selected. The dry film thickness is controlled at 70-100µm, which is suitable for the long-term erosion environment of salt spray and seawater. For high-corrosion areas such as welds, corners, fasteners, etc., the primer coating can be appropriately thickened to strengthen key protection and prevent substrate corrosion from the bottom.

    Epoxy coating

    The epoxy middle layer paint is the barrier core of the coating system, which undertakes the primer and topcoat, and plays a key role in thickening protection, blocking chloride ions, and improving the strength of the coating.The middle layer of epoxy cloud iron paint is commonly used, which contains mica iron oxide particles inside, which can form a multi-layer dense shielding structure, which effectively prevents salt spray, moisture, and chloride ions from penetrating the coating to reach the substrate, greatly improving the overall anticorrosive performance.At the same time, the middle layer of paint can fill the fine pores and construction defects of the primer coating, smooth the surface of the substrate, and improve the adhesion and flatness of the topcoat.The thickness of the standard construction dry film is controlled at 100-150µm, and the multi-layer brushing is superimposed, which can significantly improve the coating’s permeability, wear resistance, and aging resistance, and adapt to the harsh working conditions of the port.

    Marine topcoat

    Marine special topcoat is the outer protection of the coating system, facing outdoor salt spray, ultraviolet light, and wind and rain erosion, which determines the appearance durability and long-term anticorrosive stability of the equipment.Aliphatic polyurethane topcoat or fluorocarbon topcoat are preferred for port cranes. They have super UV aging resistance, salt spray resistance, scouring resistance, and self-cleaning properties. They can resist extreme marine environmental erosion for a long time and are not easy to change color, pulverize, and crack.The thickness of the dry film of the topcoat is controlled at 60-100µm, and the surface is smooth and dense after molding, which can effectively block the intrusion of external corrosive media. At the same time, it has dust-proof and salt-proof effects, greatly reducing the difficulty of late cleaning and maintenance, and ensuring the long-term stable operation of the coating system.

    Coating inspection

    Standardized coating inspection is a key link to ensure the quality of anticorrosive construction and avoid late anticorrosive failure, which runs through the whole process of coating construction.During the construction process, the dry film thickness of the primer, middle paint, and top paint needs to be tested one by one to ensure that the thickness is up to standard, the coating is uniform, and there are no leakage, thin coating, and accumulation problems.After the coating is cured, an electric spark detector is used to detect the integrity of the coating and investigate hidden defects such as pinholes, bubbles, and cracks.The adhesion tester is used to detect the binding strength of the coating to eliminate the hidden dangers of coating shedding.At the same time, the salt spray resistance and aging resistance of the coating are regularly sampled, construction and testing data are recorded, and a complete quality traceability system is formed to ensure that the entire anticorrosive coating system meets the port’s long-term protection standards.

    Maintenance Strategies for Saltwater-Exposed Cranes

    High-quality design and coating are the foundation, and normalized and standardized operation and maintenance are the key to prolong the anti-corrosion life of the crane and eliminate the hidden dangers of corrosion.Port equipment has been in a dynamic corrosion environment for a long time, and coating aging, salt accumulation, and component wear cannot be completely avoided. Only by establishing a normalized maintenance mechanism, removing corrosion triggers in a timely manner, and repairing minor damage can small corrosion be prevented from turning into major failures, and the long-term stable operation of the equipment can be guaranteed.

    Salt removal

    Salt accumulation is the core source of continuous corrosion. Salt accumulation on the surface, crevices, and inside the equipment of port cranes will continue to precipitate chloride ions, accelerating metal corrosion and coating aging.Therefore, regular desalination is the basic work of daily operation and maintenance. After the daily operation is over, high-pressure water is used to rinse the exposed surfaces of the equipment, steel structure gaps, and mechanical parts gaps to remove surface salt dust and sea water residues.Every week, the dead corners of electrical equipment, hydraulic components, and fasteners are finely wiped and desalinated to avoid salt accumulation.After the rainy season, typhoons, and high tides of seawater, all-round desalination and cleaning should be carried out immediately to eliminate the residues of saline stagnant water and cut off the causes of corrosion from the source.After cleaning, it is necessary to ensure that the equipment is completely dry to avoid the humid environment from exacerbating corrosion.

    Coating inspection

    The coating is the protective coat of the equipment. The normal inspection can detect the hidden dangers of aging and damage of the coating in time, and repair it in advance to avoid corrosion of the substrate.Formulate a hierarchical inspection system, visually inspect the exposed coating of the equipment daily, and investigate the problems of peeling, cracking, shedding, chalking, and discoloration.Focus on inspecting the coating of high-incidence areas such as welds, corners, bases, and the periphery of moving parts every month.Professional instruments are used every quarter to test the thickness, integrity and adhesion of the coating.For minor scratches and paint spots, do local patching and repair in time.For large-area aging and failed coatings, timely polishing and re-coating are used to prevent the expansion of the damaged area of the coating and protect the substrate from erosion.

    Component lubrication

    Precise lubrication is the core means of anticorrosion and wear reduction of moving parts. Grease can form a protective oil film on the moving surface of the metal to isolate salt spray and moisture erosion, while reducing friction and wear of parts.For bearings, gears, pins, pulleys, guide rails and other moving parts, special marine anticorrosive greases are selected, which have the characteristics of salt spray resistance, water erosion resistance, and long-term stability.Formulate a standardized lubrication cycle, add grease to high-frequency operating parts every month, and fully change oil to low-frequency parts every quarter.Before lubrication, the surface area of the parts must be thoroughly cleaned of salt, rust, and impurities to avoid impurities from mixing into the lubricating layer and causing wear and corrosion, so as to ensure that the oil film completely covers the metal surface, and realizes the dual effects of anti-corrosion and wear reduction.

    Damage repair

    Timely repair of corrosion damage is the key to curbing the spread of diseases. If minor corrosion is left alone, it will quickly spread into structural corrosion failures.Enterprises should establish an equipment operation and maintenance mechanism for timely maintenance, complete rust removal and desalination operations in time for dot-like rust and surface oxidation problems on the surface of the equipment, and install matching anticorrosive coatings.In view of problems such as component wear and abnormal mating gaps, timely equipment maintenance and parts replacement will be carried out.In view of hydraulic leakage, oxidation of electrical contacts and other faults, clean and repair equipment in time, replace aging accessories and sealing structures.For steel structure wall thickness loss, weld corrosion and other issues, through structural reinforcement, welding and re-anticorrosive treatment, the development of corrosion diseases is controlled, and the overall structure of the equipment is guaranteed to be complete and the operation is stable.

    How to Build a Long-Term Corrosion Protection Strategy

    The seawater anticorrosion of port cranes is not a one-time construction or short-term maintenance work, but a system engineering that runs through the whole life cycle of the equipment.Short-term anticorrosion can only solve surface problems. Only by building a long-term anticorrosion strategic system that adapts to the working conditions of the port and meets the needs of the equipment can long-term equipment protection, the lowest life cycle cost, and the highest operating safety factor be achieved, and the stable production of the port can be escorted.

    Site assessment

    Site working condition assessment is the basis of a long-term anticorrosive strategy. The salt spray concentration, humidity, seawater tides, and wind working conditions of different ports vary greatly, and the corrosion risk level is completely different.It is necessary to carry out a comprehensive normalization assessment of the equipment operation site, detect the concentration of salt spray chloride ions, air humidity, and seawater corrosion levels in the area, and divide the C5-M high corrosion core area and the ordinary coastal area.Count the frequency of extreme working conditions such as seasonal climate change, typhoons, heavy rains, and high tides at the site.Investigate additional corrosion causes such as site dust, sewage, industrial impurities, etc.Based on the measured data of the site, accurately match the anticorrosive design, coating system, and operation and maintenance frequency to eliminate insufficient protection or waste of resources caused by the unified protection plan.

    Protection levels

    Combined with the evaluation results of on-site working conditions, port cranes need to adopt a differentiated and hierarchical anti-corrosion control model to avoid waste of resources or insufficient protection caused by unified protection.For the core load-bearing and operating components such as steel structures and main control electrical systems, high-standard anti-corrosion configuration and high-frequency inspection and monitoring are implemented.For key components such as hydraulics, transmissions, and key fasteners, special anticorrosive structures and regular special maintenance are used.The auxiliary structure of the equipment implements conventional anti-corrosion standards.This hierarchical protection method can rationally allocate operation and maintenance resources, while stabilizing the anticorrosive effect, it can effectively improve the overall economy of equipment operation and maintenance.

    Integrated protection

    Integrated and comprehensive protection is the core logic of long-term anticorrosion. It breaks the limitations of single coating and single maintenance, and builds an all-round integrated anticorrosion system covering structural design, material selection, coating protection, daily operation and maintenance, and intelligent monitoring.Complete the optimization of the anticorrosive structure in the equipment research and development stage to avoid the hidden dangers of corrosion from the source.Through anticorrosive materials and multi-layer protective coatings, a stable static protective barrier is formed, and dynamic operation and maintenance protection is realized by combining normalized cleaning, lubrication, and repair.With the help of intelligent monitoring system, real-time risk early warning is realized.Multi-dimensional protection cooperates with each other, complements each other and enhances efficiency, completely solves the limitations of a single protection method, and realizes a long-term anticorrosive effect with all-round and no dead ends.

    Crane customization

    Customized anti-corrosion solutions are adapted to different types and working conditions of port cranes to improve the accuracy and adaptability of protection.Different models of port gantry cranes, gantry cranes, shore bridges, tire cranes, etc. have large differences in structural layout, operating scenarios, and exposure levels, and different areas with high corrosion incidence.Special anti-corrosion customization is made for different models, and the design of salt spray protection and stagnant water drainage is strengthened for offshore operating models.The operating models in the tidal zone are thickened for underwater and tidal zone coating protection.High-frequency operating models strengthen the wear-resistant and anticorrosive design of moving parts.At the same time, according to the customer’s operation intensity and service life requirements, customized differentiated anti-corrosion configurations can be maximized to adapt to actual operation scenarios.

    Lifecycle cost

    The whole life cycle cost control is the core goal of the long-term anticorrosive strategy. The core value of anticorrosive protection is not simply to reduce the initial investment, but to significantly reduce the loss of late maintenance, replacement, and downtime.Short-term low-cost anti-corrosion solutions often have short-term protection, coating failure and component corrosion will occur in 1-2 years, and the comprehensive cost of frequent maintenance and replacement is extremely high.The standardized and systematic long-term anticorrosive program has a moderate increase in early investment, but it can extend the anticorrosive life of the equipment to 8-15 years, significantly reduce the failure rate, maintenance frequency, and component replacement costs, and reduce the loss of downtime and missed work.Through the whole life cycle cost accounting, balance the early anti-corrosion investment and the later operation and maintenance costs to maximize the economic and safety benefits of the equipment.

    Henan Mine Crane Factory Custom

    Seawater salt spray corrosion is the main cause of aging of port crane equipment, frequent failures, and rising operation and maintenance costs.Equipment anticorrosion cannot rely on a single touch-up paint or post-mortem maintenance. It needs to combine the characteristics of easily corroded components, equipment anticorrosive structure design, multi-layer protective coating technology, normalized maintenance and maintenance, and full-cycle protection strategies to form a complete anticorrosive system.Multi-dimensional collaborative control can effectively resist corrosion and damage in marine working conditions and stabilize the operating state of the equipment.

    Henan Mine Crane Factory  is a professional port crane manufacturer. We provide customized anticorrosive equipment and complete protection solutions for marine high-salt corrosion conditions.From the selection of raw materials, the optimization of structural anticorrosion, to the construction of professional marine coatings, and the guidance of late operation and maintenance, the whole process is tailored to the port operating environment to create high-corrosion-resistant equipment.Help users significantly reduce equipment failure rates and maintenance costs, extend equipment service life, and ensure long-term stable and efficient operation of terminal lifting operations.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Optimize Your Warehouse Layout with the Right Overhead Crane

    How to Optimize Your Warehouse Layout with the Right Overhead Crane

    How to Optimize Your Warehouse Layout with the Right Overhead Crane

    Warehouse layout optimization is the core of improving operational efficiency, ensuring safety and reducing costs, which directly affects warehouse turnover and profitability. The layout optimization value of overhead cranes is often overlooked, but in fact, choosing the right bridge crane and scientific layout can solve the heavy material handling problems, optimize the use of space and workflow, and improve warehouse efficiency.

    This article will be from the bridge crane basic knowledge, optimization value, practice methods, selection techniques and error avoidance, etc., to help enterprises create efficient and safe warehouse operation system.

    Understanding the Basics of Overhead Cranes

    Simply put, bridge crane is a kind of equipment that moves loads horizontally along the ceiling of the plant, different from the handling tools that move along the corridor or the ground, and its core advantage is to get rid of the restriction of the ground space.

    It has a powerful material handling capability and is mainly used for multi-directional movement of materials in industrial warehousing scenarios, loading and unloading operations in plant buildings, freight yards, train stations or ports. Operators can operate the crane by manual control, wired suspension button station, etc. Some advanced models also support wireless remote control, which is extremely flexible.

    Compared with forklifts, conveyors and other ground equipment, overhead cranes have a wider operating range and do not take up space on the ground, which is the core premise of their ability to optimize the warehouse layout.

    Components of Overhead Cranes

    In order to realize the precise matching between overhead travelling crane and warehouse layout, first of all, we need to clarify the function and role of its core components – each of them has a direct impact on the rationality, safety and efficiency of the layout.

    • Winch: as the “heart” of the crane, it is responsible for material lifting and lowering operations, and its loading capacity must be fully matched with the load demand of daily and peak operations in the warehouse, otherwise it will affect the operational efficiency, and even lead to potential safety hazards.
    • Bridge: i.e. horizontal beam, is the core component to support the winch, its span directly determines the coverage width of the crane, which in turn affects the efficiency of the utilization of the warehouse lateral space and layout planning.
    • Rail: crane bridge running track, usually installed in the plant wall or structural columns, its length determines the longitudinal running distance of the crane, directly shaping the operation process path of the warehouse, a reasonable layout of the track can reduce the redundancy of material handling.
    • Trolley: the part that drives the winch to move horizontally along the bridge, which can realize the lateral fine-tuning of the load and increase the flexibility of material placement, especially suitable for multi-position, high-density storage warehouse layout.
    • Safety components: including overload protection devices, limit switches, emergency stop buttons, etc., is the bottom line of the warehouse safety operations, but also the layout planning can not be ignored in the link, the need for these safety devices to set aside enough space to ensure that their normal operation.

    How Overhead Cranes Improve Warehouse Efficiency

    Maximize Space Utilization

    Most warehouses have the pain point of crowded ground and wasted vertical space, one of the core values of overhead cranes is to shift the center of gravity of operation to the air and tap the potential of vertical space. By lifting vertically and moving materials horizontally, it frees up more space for storage and turnover without occupying floor aisles.

    With its lifting capacity, warehouses can build higher shelves to achieve high-level stacking, without expanding the footprint while increasing storage capacity; in small warehouses, it can also be used to reduce the width of the racking aisle, eliminating the dead zone on the ground, and realizing the efficient use of space.

    Optimization of Operation Flow

    The core operation process of the warehouse covers the four major aspects of receiving, storing, picking and shipping. By scientifically planning the layout of the bridge crane, it can realize the seamless connection of the various aspects, quickly complete the material transfer, and effectively avoid ground congestion and ineffective movement problems;

    At the same time, the planning of special operation paths can further reduce the interference of equipment and personnel, crack the operational bottleneck, and significantly improve the operational efficiency of the warehouse and the speed of supply chain turnover.

    Cost Reduction

    Although the initial investment in overhead cranes is relatively high, the cost savings are significant from a long-term operational perspective. It can effectively replace the manual labor required for heavy material handling, optimizing the allocation of human resources and devoting employees to higher-value operations;

    At the same time, by virtue of accurate and stable operational performance, it significantly reduces material damage and loss, reduces safety accidents and additional costs brought about by equipment failure and downtime, and helps enterprises realize long-term stable profitability.

    Improve Safety

    Bridge cranes can effectively reduce the frequency of ground operation equipment and manual handling, significantly reducing the risk of workplace accidents and equipment collision; it is equipped with overload protection, collision warning and other professional safety devices to ensure that the work process is in line with the industry safety standards, for hazardous materials operation scenarios, but also through the remote control mode, to further build a strong line of defense for the safety of personnel and property.

    Best Practices for Integrating an Overhead Crane Spatial Planning and Strategic Layout of Cranes

    Space planning is the core of overhead travelling crane layout, which should be centered on “no dead-angle coverage, no interference operation”: combining the warehouse size, material distribution and operation frequency to determine the installation location, eliminating the handling dead zone;

    reasonably planning the location of the track and other equipment, reserving a safe distance to avoid collision; accurately matching the track layout with the warehouse size to shorten the handling distance and reduce the redundant links. Shorten the handling distance and reduce redundant links.

    Optimize the Operation [rocess

    Crane design needs to be bound with the depth of the warehouse operation process, around the receipt, storage, picking, delivery planning operation path, to avoid cross operation and ineffective movement; can be designed as a straight line path through the core operation area, reducing secondary handling. At the same time, according to the type of material to choose the appropriate accessories, and planning for special operating areas, to ensure smooth processes, improve operational accuracy and safety.

    Safety and Maintenance Considerations

    Safety and maintenance is the key to the long-term stable operation of cranes, the layout needs to reserve sufficient operating and emergency channels for operators; planning convenient maintenance and repair channels, to facilitate the daily maintenance of core components, reduce maintenance costs and downtime;

    at the same time, set up a safety warning zone in the operating area, clear boundaries, prohibit unrelated personnel from entering, and strengthen the safety of operations.

    Technology Integration

    Combining advanced technology can further optimize the warehouse layout and enhance operational efficiency: adopting wireless remote control, touch screen and other advanced control systems to enhance operational flexibility;

    docking the crane with the warehouse management system (WMS) to achieve operation and inventory management linkage and reduce manual intervention; introducing automation technology for repetitive operations to achieve automatic positioning and handling, releasing manpower and enhancing optimization results.

    How to Select the Right Warehouse Overhead Crane

    Assessing Your Warehouse Requirements

    The premise of choosing overhead cranes is to clarify the actual needs of the warehouse, to avoid improper selection leading to unreasonable layout and low operating efficiency.

    • Load capacity: first determine the average load and peak load of the warehouse daily operation, calculate the maximum lifting weight of the crane according to the formula of “peak load×safety coefficient (1.25-1.5)”, and at the same time, select the winches, ropes or chains that match the load demand to prevent overloading and prevent the safety and service life of the equipment. operation, to protect the safety and service life of the equipment.
    • Span and coverage: the span of the crane needs to be matched with the width of the warehouse, when the warehouse is narrower, you can choose a single girder crane, and when it is wider, you need to choose a double girder crane; the length of the track needs to be determined according to the length of the warehouse, to ensure that the crane’s operating distance to cover all the operating areas, and at the same time, combined with the height of the crane hooks and the headroom under the hooks, the height of the shelves is reasonably planned, to avoid affecting the stacking of materials and the Crane operation.
    • Frequency of operation and working level: According to the frequency of daily operations in the warehouse, select the appropriate crane working level in accordance with ISO or CMAA standards – high frequency of operations, large load warehouse, you need to choose a higher level of crane to ensure that the equipment can run stably for a long time to reduce the risk of failure. Warehouse environment: The warehouse environment needs to be fully considered.
    • Warehouse environment: the environmental conditions of the warehouse need to be fully considered, high temperature, high humidity environment need to choose corrosion-resistant, heat-resistant crane materials; dust, chemicals, explosive environment needs to be equipped with special safety protection devices to ensure that the crane can adapt to the environmental needs, to avoid equipment damage and safety accidents.

    Choose the Right Crane Configuration

    The configuration of the crane directly affects its adaptability to the warehouse layout, and should be accurately selected according to the needs of the warehouse:

    • Single girder and double girder selection: single girder crane structure is simple, low cost, suitable for warehouse width is narrower, lighter load scenarios; double girder crane load capacity is stronger, span is larger, suitable for warehouse width is wider, heavy material handling scenarios, according to the size of the warehouse and the load demand selection.
    • Attachment selection: choose the appropriate attachment according to the type of material, such as handling steel, metal products can choose electromagnetic suction cups, handling plates, boxes can choose special fixtures, handling of ordinary goods can choose standard hooks, through the optimization of attachments to enhance the efficiency and safety of material handling.
    • Control system selection: manual control is suitable for small warehouses, low operating frequency of the scene; wireless remote control is suitable for large warehouses, complex layout, can enhance the flexibility of the operation; automation control system is suitable for high frequency of operation, repetitive scene, can reduce manual intervention, improve efficiency.

    Installation and Maintenance Considerations

    The installation and maintenance planning of the crane directly affects its long-term operational efficiency and the stability of the layout. In the installation phase, the track layout needs to be optimized to minimize the redundant aspects of material handling and ensure that the crane can be quickly adapted to the warehouse workflow after installation;

    At the same time, choose a professional installation team to ensure that the equipment is installed in a standardized manner to avoid safety hazards and operational failures caused by improper installation. In the maintenance phase, it is necessary to develop a comprehensive daily maintenance program, regular lubrication, inspection and replacement of the core components of the crane, and timely detection of hidden faults;

    Choose a supplier with technical support and spare parts supply capability to ensure that maintenance support can be obtained quickly when the equipment fails, reducing downtime and guaranteeing the smooth operation of the warehouse layout.

    Common Mistakes to Avoid When Setting Up Overhead Cranes in Your

    When many enterprises introduce overhead cranes to optimize the warehouse layout, due to the lack of professional planning, it is easy to fall into the following misunderstandings, resulting in irrational layout, inefficient operation, and even lead to potential safety hazards:

    • Underestimation of crane load capacity: Choosing a crane with insufficient load capacity to save costs will not only lead to low operational efficiency and fail to meet the handling needs of heavy materials, but also cause equipment overloading, failure, and even safety accidents, resulting in greater economic losses and schedule delays.
    • Neglect of traffic flow: the layout planning does not fully consider the crane’s operating path and ground operating equipment, personnel traffic flow, resulting in crane and forklift, conveyor and other equipment congestion, the formation of operational bottlenecks, reducing the overall warehouse efficiency.
    • Ignoring safety standards: not in accordance with industry safety standards planning crane installation and operation area, not equipped with the necessary safety protection devices, or not reserved enough safe space, easy to cause equipment collision, casualties and other safety accidents, while may face regulatory penalties.
    • Neglect of maintenance needs: layout planning without reserving maintenance access, or not formulate a comprehensive maintenance plan, resulting in inconvenient crane maintenance and overhaul, easy to equipment failure, increase unplanned downtime, affecting the continuity of warehouse operations, while enhancing long-term operating costs.
    • Disconnect between cranes and operation process: the selected crane configuration, installation location and warehouse operation process does not match, resulting in redundant material handling links, unable to realize the seamless integration of various links, wasting space and labor costs, unable to achieve the purpose of layout optimization.

    Conclusion

    To sum up, bridge crane is a strategic tool to optimize warehouse layout and enhance operational efficiency, and its core value lies in the efficient use of vertical space, optimization of workflow, cost reduction, safety, and helping enterprises to maximize warehouse efficiency.

    To play its role, we need to clarify the core components of the equipment, combined with the needs of the warehouse scientific layout, accurate selection, avoid misunderstandings and do a good job of safety and maintenance; enterprises can combine their own situation to invest, do not have the conditions for long-term investment, you can choose to crane leasing, to achieve optimization of the layout and cost control win-win.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Operate an STS Crane in an Automated Port: Complete Operator Guide

    How to Operate an STS Crane in an Automated Port: Complete Operator Guide

    How to Operate an STS Crane in an Automated Port: Complete Operator Guide

    Ship-to-shore (STS) cranes move the vast majority of containers handled at the world’s busiest ports, and how well they’re operated directly determines vessel turnaround time.

    As terminals shift toward automation, the skills required to run these cranes have changed operators now manage sensors, PLCs, and remote consoles as much as joysticks. This guide walks through exactly how to operate an STS crane in an automated port, from the basic mechanical cycle to remote operating stations, safety interlocks, and training pathways.

    Whether you’re onboarding a new operator, upgrading a terminal’s automation stack, or evaluating ROS technology, this article covers the full operational picture including gaps left by most existing guides on training workflows and troubleshooting.

    What Is an Automated STS Crane?

    An automated STS crane (also called an automated quay crane) is a rail-mounted gantry crane that loads and unloads containers between a vessel and the quay using computer-controlled systems instead of full manual operation. Modern units combine PLCs, motion controllers, and sensor arrays to manage hoisting, trolley travel, and gantry movement with minimal human intervention.

    Automation exists on a spectrum:

    • Manual: operator controls every movement from an onboard cab
    • Semi-automated: operator-assisted with anti-sway and auto-positioning support
    • Remote-operated: operator controls the crane from a control room via a Remote Operating Station (ROS)
    • Fully autonomous: the crane executes pre-programmed cycles with human supervision only

    Most “automated ports” today run on the semi-automated or remote-operated model rather than fully autonomous cranes, since human oversight remains a regulatory and safety requirement at nearly every major terminal.

    How Automated STS Cranes Work

    Every STS crane lift automated or manual follows the same basic sequence:

    • Portal Crane Walking Alignment: The portal crane moves along the wharf track as a whole, accurately adjusts the position of the whole machine, completes the alignment calibration with the berth of the ship, and lays the foundation for the subsequent container operation.
    • Accurate positioning of the trolley: the lifting trolley is adjusted to make lateral displacement along the boom, driving the spreader to move smoothly and accurately stop at the position directly above the target container to ensure that the center of the lifting point is aligned.
    • Spreader lifting and lowering in position: after completing the positioning, the spreader descends vertically and smoothly to fit the top surface of the container, and enters the locking and docking preparation state.
    • Twist lock locking fixation: the twist locks at the four corners of the spreader are automatically rotated and clamped, firmly locking the steel castings at the four corners of the container, realizing the rigid connection between the spreader and the container, and eliminating the risk of slipping off during the lifting.
    • Container lifting and transferring: after locking confirmation, the container will be lifted at a constant speed, and the horizontal transfer will be completed with the lateral alignment of the trolley, and finally it will be smoothly dropped to the transportation chassis, AGV trolley or the designated position in the yard.

    In an automated cycle, sensors and cameras verify alignment at each stage, and the PLC will not proceed to the next step until corner-by-corner confirmation is received a critical safety gate, covered in more detail in Section 4.

    Key Components Operators Must Understand

    You don’t need to be an electrical engineer to run an automated STS crane, but operators and supervisors should understand what each system is doing:

    • Spreader and Twist Lock: Equipped with telescopic spreader, it can be flexibly adapted to the operation of 20-foot, 40-foot and 45-foot standard containers; with the automatic twist lock structure, it can accurately lock the corner pieces of the containers to ensure the stability and safety of the lifting connection.
    • Drive system: adopts independent drive structure, which controls the operation of boom, trolley travel, lifting, gantry and other mechanisms respectively, with each action starting and stopping independently without interfering with each other, which is suitable for the operation logic of non-synchronized operation of the equipment.
    • Position feedback sensor: relying on laser detection and encoder fusion positioning system, it can track the dynamic position of the spreader relative to the container and the ship’s cabin rail in real time with high precision, providing data support for precise alignment operation.
    • Anti-swing control: Equipped with professional anti-swing control algorithm, through input shaping, active disturbance suppression and other core technologies, it can effectively offset the load swing generated during the running process of the trolley, and greatly improve the smoothness of lifting and operational efficiency.
    • Communication network: using fiber optic transmission or highly reliable wireless communication links, real-time, stable transmission of control commands, operating screen and other core data between the crane and the control room, to ensure efficient and accurate remote control.

    Step-by-Step: How to Operate an STS Crane in an Automated Port

    This is the practical operating sequence a crane operator or remote operator follows in a semi-automated or remote-operated terminal:

    1. Pre-operation checksreview crane status dashboard for fault codes, wind speed readings, and any maintenance flags before starting a shift
    2. Receive the work order from the TOSthe Terminal Operating System assigns a bay and container sequence to the crane
    3. Position the gantryeither drive manually or confirm the automated gantry alignment to the correct vessel bay
    4. Engage trolley/hoist for pickupguide or confirm the trolley’s automated positioning over the target container
    5. Verify twistlock engagementthe PLC will only authorize hoisting once all four corner sensors confirm a secure lock; if any lock fails, the system holds and alerts the operator
    6. Monitor the lift and transferwatch anti-sway behavior and camera feeds as the container moves from ship to shore (or vice versa)
    7. Confirm placementverify the container lands correctly on the chassis, AGV, or yard equipment before releasing twistlocks
    8. Log the move and repeatthe TOS updates automatically, and the crane proceeds to the next assigned container

    Throughout this cycle, the operator’s role shifts from “driving” the crane to supervising and intervening stepping in only when sensors flag a misalignment, fault, or unsafe condition.

    Remote Operating Stations (ROS): The New Control Room

    One of the biggest operational shifts in automated ports is the move from onboard cabs to Remote Operating Stations. Instead of sitting in a cab suspended above the quay, operators work from an ergonomic desk in a control room, often managing multiple cranes in rotation.

    A typical ROS setup includes:

    • Multi-screen video monitoring wall: integrated multi-channel visual display interface, real-time synchronous display of spreader close-up, boom conditions, dock wide-angle and other multi-channel camera images, all-round coverage of the operating field of view, helping operators to grasp the site dynamics in real time.
    • Joystick and touch control dual-control system: following the logic of the native crane console layout, with the joystick physical control + touch screen intelligent control dual-mode, adapted to the operator’s original operating habits, reduce the cost of getting started, to ensure the smoothness of control.
    • Intelligent status dashboard: real-time refreshing equipment operating parameters, fault warning alarms, operational productivity and other core indicators, data visualization is clear and intuitive, easy to troubleshoot and control the progress of operations.
    • Low-latency encrypted communication link: Adopting encrypted fiber optic or wireless exclusive transmission channel, effectively avoiding the risk of data interference and information leakage, and stably transmitting the control commands and operation data with ultra-low latency to ensure the precision, real-time and safety of remote control.

    This setup improves operator safety (removing them from height, weather, and noise exposure) and allows one operator to support several cranes depending on automation level directly improving labor efficiency at scale.

    Automation Technologies Powering the Cycle

    Several technologies work together behind the scenes to make automated operation possible:

    • PLC-based interlocks: prevent unsafe sequences (e.g., boom and trolley never move simultaneously; hoist and gantry are similarly isolated)
    • Anti-sway compensation: uses real-time feedback to smooth trolley acceleration and deceleration, reducing payload swing
    • Vision systems: confirm twistlock alignment and detect container positioning errors before lift authorization
    • Zone-based anti-collision systems: divide the quay into zones per crane, with lidar/radar sensors and PLC interlocks preventing two cranes from entering the same working area
    • TOS/CMS integration: connects crane-level execution to terminal-wide workflow planning, optimizing job sequencing across the yard

    Safety Protocols and Anti-Collision Systems

    Safety in automated STS operation relies on layered redundancy rather than any single system:

    • Twist lock verification protection mechanism: the system is equipped with twist lock safety verification logic, which must confirm that the four corners of the container twist locks are completely locked and the status is compliant before starting the lifting operation, and will automatically intercept the lifting operation if the locking is not completed to eliminate the risk of falling out of the container.
    • Wind speed safety monitoring system: real-time monitoring of the site environmental wind speed, when the wind speed exceeds the threshold for safe operation of the equipment, the system will automatically limit the equipment action or forced shutdown, to avoid the lifting of the windy conditions of deflection, overturning and other safety hazards.
    • Independent anti-collision protection hardware: Equipped with independent anti-collision detection equipment such as LIDAR and radar, it does not rely on the operation of the main automation system, and even if the equipment is switched to manual operation or manual intervention, the anti-collision protection function is still continuously online, which guarantees the safe operation of the equipment throughout the whole process.
    • Remote identity verification and authority control: The remote control system has a built-in perfect identity authentication and authority management mechanism, which strictly screens the operator’s authority, and only authorized personnel can issue equipment operation instructions, effectively eliminating illegal manipulation.
    • Encrypted exclusive communication channel: the use of encrypted transmission links to build a communication bridge between the crane and the remote control room, can effectively resist illegal access, data theft, while avoiding external signal interference, to ensure stable, safe and accurate transmission of control instructions.

    These layers matter because automated systems still fail occasionally the goal is to ensure no single point of failure can cause a serious incident.

    Operator Training and Simulation for Automated Cranes

    Training has evolved alongside automation. Rather than learning entirely on live equipment, most terminals now train operators on full-mission simulators that replicate ROS hardware and real load physics before any hands-on crane time.

    Effective training programs typically progress through:

    1. Theoretical instruction: crane principles, safety procedures, and port operational workflows
    2. Coordination assessment: testing hand-eye-foot reflexes relevant to joystick and pedal control
    3. Simulator practice: realistic cable tension, sway behavior, and twistlock mechanics under varied weather and fault conditions
    4. Live equipment certification: supervised operation on the actual crane before independent sign-off

    Simulator-based training reduces wear on live equipment, allows practice of rare fault scenarios safely, and shortens the time to full operator proficiency a meaningful advantage as automated terminals scale up staffing.

    Productivity Benchmarks and Data

    Crane productivity is typically measured in moves per hour (MPH) the number of container lifts completed per crane per hour. Global average gross crane productivity has been benchmarked around 26 moves per hour, a figure widely used as a baseline when modeling terminal throughput and vessel turnaround scenarios.

    Automated and remote-operated cranes aim to improve consistency more than raw peak speed: sensor-driven cycles maintain a steady pace across shifts, reducing the variability caused by operator fatigue that affects fully manual operations. For port planners, this predictability is often as valuable as raw speed, since it makes vessel scheduling and berth allocation more reliable.

    Common Challenges and Troubleshooting in Automated STS Operation

    Even well-automated cranes run into operational friction. Common issues include:

    • Twistlock misalignment: usually resolved by fine trolley/spreader adjustment guided by corner cameras; persistent failures require sensor recalibration
    • Communication latency or dropout: fiber-optic backups and redundant wireless channels mitigate this, but operators should know manual fallback procedures
    • Wind-related operational holds: automated wind cutoffs are a safety feature, not a malfunction; operators should plan job sequencing around forecasted wind windows
    • Drive/motor degradation: most STS cranes use dual-motor hoist drives specifically so operation can continue at reduced speed if one drive fails, avoiding full downtime
    • Zone interlock conflicts: when two cranes’ work zones overlap unexpectedly, regional control centers can override and reassign zones to keep operations moving

    Understanding these failure modes and the manual fallback for each is what separates a merely certified operator from one who can keep an automated terminal running smoothly under real-world conditions.

    Conclusion

    With the iterative upgrading of automated terminals, STS shorebridge has bid farewell to the traditional manual operation and stepped into the intelligent mode of sensor detection, safety interlocking and remote control. The core of competition in the industry has also changed to the ability of personnel to use the equipment “mechanical + digital” system, relying on intelligent control technology and factory and enterprise synergy, which can effectively improve the efficiency and safety of port operations.

    Terminal automation upgrades and personnel training landing, inseparable from the mature R & D and engineering capabilities of the cooperative manufacturers. Henan Mine Crane, which is deeply engaged in the field of lifting equipment, can provide an integrated solution of equipment adaptation and system upgrading to help terminals smoothly realize the transformation of intelligent and remote operation.

    If your terminal is evaluating the automation transformation path or personnel capacity upgrading program, now is the key stage to plan the technical route and implementation practice together.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Operate a Bridge Crane Safely: Essential Precautions

    How to Operate a Bridge Crane Safely: Essential Precautions

    How to Operate a Bridge Crane Safely: Essential Precautions

    Bridge cranes are commonly used heavy-duty lifting equipment in manufacturing, warehousing, factories and engineering fields. They have high heavy-duty handling efficiency, but they are high-risk special equipment.Its structure is complex, the load is large, the operation is wrong, the inspection is not in place or the maintenance is missing, and it is prone to falling objects, equipment damage, casualties and shutdown accidents.

    Based on international safety standards such as OSHA and ASME B30 and original factory specifications, this article combs the main safety risks of bridge cranes, pre-shift inspections, operating specifications, maintenance, emergency response, common violations, and equipment safety design points to provide practical guidance for enterprise lifting safety management.

    Understand the Main Safety Risks of Bridge Cranes

    Most of the safety accidents of bridge cranes originate from predictable and unavoidable risks and hidden dangers, which are mainly concentrated in the four dimensions of improper load operation, material swing and fall, mechanical and electrical equipment failure, personnel operation and on-site environment. Accurate identification of risks is the basis for safe production.

    Overload and load risk

    Overload is the most important safety hazard of bridge cranes.Exceeding the rated safe working load (SWL) and exceeding the working level will cause deformation of the main beam, overload of the mechanism, derailment, and structural fracture and collapse in severe cases.

    The center of gravity of the load is skewed and the binding is not strong, which will produce additional dynamic loads and damage the equipment.The selection of the spreader rigging is wrong or damaged, and the spreader is prone to fracture and material slippage.The total weight of materials and spreaders must be calculated before hoisting, and it is forbidden to estimate the load empirically.

    Load swing and falling object risk

    The load swing is mostly due to emergency start and stop, cable-stayed crane, unbalanced load, strong wind, and excessive operating speed.Swinging cargo will hit the plant and equipment, threaten the safety of personnel, and cause the crane to capsize and the track to be damaged in severe cases.During operation, it should be operated smoothly, the load attitude should be controlled, and the traction rope should be used if necessary.

    Risk of electromechanical failure

    Wear and failure of core components such as hoists, brakes, wire ropes, hooks, limit switches, etc. can cause rushing, falling objects, and slipping cars.Electrical faults such as aging of the line, failure of the remote control, and abnormal voltage can cause the equipment to get out of control.Most mechanical and electrical failures gradually deteriorate, and preventive maintenance can investigate hidden dangers in advance.

    Personnel environmental risk

    Undocumented induction, insufficient training, and illegal operation are the main human-caused causes of the accident.Poor vision, insufficient light, and confusion in command and communication can easily lead to operational errors.There are many obstacles on the scene, the area is crowded, and unrelated personnel enter the hoisting area, which is prone to collisions and injuries.High temperature, dust, and corrosive environments will also accelerate the aging of components.。

    Pre-Operation Safety Inspection

    Before each start-up operation and before the start of each shift, all-round inspections of bridge cranes must be strictly implemented, and the four modules of structure, lifting components, safety devices, and operating environment must be investigated one by one, and inspection records must be made. If defects are found, immediately stop for rectification, and the equipment is strictly prohibited from operating with faults.

    Main structure inspection

    Focus on inspecting the main beam, end beam, operating track, connecting bolts, welding parts and support structure of the crane.Carefully investigate whether there are cracks, deformation, bending, corrosion and aging problems in the main structure, and confirm that all connecting fasteners are not loose or missing, and the track is not offset, worn, deformed, or damaged by bumps.At the same time, check the connection parts of the equipment to ensure that the overall structure is stable and there are no structural safety risks.

    Inspection of lifting accessories

    The lifting parts are the core of the carrying material, and they need to be refined one by one: check whether the hook has cracking, distortion, and excessive wear, and whether the anti-release buckle of the hook is intact and tightly closed; check whether the wire rope/chain has broken wires, kinks, deformation, corrosion, tensile wear, etc., and replace it immediately if it meets the scrap standard.

    At the same time, check the working conditions of the reel and pulley, and confirm that the wire rope is arranged in a regular manner, no slotting, and no blocking; test the braking performance of the brake to ensure that the braking is sensitive and the locking is stable.;

    Finally, check all lifting accessories such as slings, beams, shackles, etc. To confirm that the rated bearing capacity of the accessories is up to standard, the appearance is intact, and the specifications match, so as to prevent the use of damaged, unmarked, and non-standard accessories.

    Safety device test

    Start the no-load test of all control devices to verify that the handle, wireless remote control, and cab control system are responsive and accurate in action, without caton, delay, or loss of control.Focus on testing the emergency stop device to ensure that the operating power of the equipment can be cut off instantly and emergency braking can be achieved.

    Verify the upper and lower stroke limit switches and operating limit devices one by one to ensure that the limit is accurate and effective, and to prevent topping and over-range accidents; test the safety warning equipment such as alarm horns, warning lights, and anti-collision devices to ensure normal operation; and finally test the walking brake and lifting motion system to confirm that there is no offset, no slippage, and no abnormal lag in braking.

    Operating environment inspection

    Clean up all obstacles in the crane operation track and ground operation area in advance to ensure that the operation path of the cart and trolley is smooth throughout the process.Strictly delineate the isolation area for hoisting operations, set up a no-entry area under the floating operation path of the material, place warning signs and protective fences, and strictly prohibit unrelated personnel from entering the scope of the operation.

    Confirm that the work site is well-lit and has a clear field of vision. Outdoor operations need to investigate the effects of severe weather such as wind, rain and high winds; confirm in advance that the on-site command and operator communication channels are smooth, the operator’s position is safe, and the safety line of defense for on-site operations is fully strengthened.

    Safe Operating Practices for Bridge Cranes

    Load control

    All operations must strictly follow the rated safety load of the equipment, and overloading operations and over-working conditions are strictly prohibited.When calculating the hoisting load, all the material weight, lifting accessories weight, and dynamic shaking load must be included in the calculation, and the equipment nameplate and load parameter table must be accurately checked.Under special and complex working conditions, the equipment load needs to be derated to eliminate all lucky operations and avoid the risk of overload from the source.

    Standard lifting

    Before lifting, the hook must be accurately aligned directly above the center of gravity of the material to ensure vertical force, and illegal operations such as cable-stayed, diagonal hoisting, dragging materials, and violent hoisting must be resolutely eliminated.

    When lifting, slowly tighten the sling to eliminate the slack of the rope. After the material is slightly off the ground, the attitude is stable, and the force is balanced, the height will be steadily raised and the transfer operation will be carried out.Standard binding and hoisting processes are used throughout the process to ensure that the material is evenly forced and firmly bound.

    Control pendulum load

    During the operation of the equipment, sudden acceleration, emergency braking, and instantaneous reversing are prohibited to avoid the material swinging violently due to inertia.The whole process adopts a smooth and gradual control method, and the equipment equipped with a frequency conversion drive device can use the characteristics of the equipment to achieve uniform speed operation and minimize material shaking.

    Plan the transfer path in advance before the operation, and maintain a safe distance from the plant structure, peripheral equipment, and pipelines during operation. Large-scale material hoisting can be assisted by traction ropes to stabilize, completely avoiding the risk of material swing and collision.

    Regional control

    Operating principle: It is strictly forbidden for floating materials to pass above the personnel, and the path must be adjusted in advance if it can be avoided.The personnel in the operation area are controlled through warning lights, alarm sound effects, protective fences, and special supervision throughout the process.

    Strictly implement the principle of “No standing under the material”, and under any circumstances, operators are prohibited from standing, operating, and passing under the floating material.If you need to enter the work area, you must first land the material safely and fix it firmly.

    Communication management

    On-site operations must adopt national standard standardized gesture signals or special radio communication equipment to ensure that the instructions of the operator and the command staff are unified and transmitted accurately.When the field of vision of the operation is limited and there is a visual blind spot, it is necessary to set up a unique and exclusive command staff to eliminate the problem of multiple people commanding and confusing instructions.

    The instruction information is confirmed in real time throughout the operation. Once the communication is interrupted and the instruction is blurred, the operation will be stopped and suspended immediately, and the construction can continue after it is restored unobstructed.

    Safety Precautions for Different Crane Movements

    Lifting operation

    The material lifting process should start and stop smoothly, rapid lifting and instantaneous braking are strictly prohibited, and the attitude of the crane and the operating status of the wire rope should be observed in real time, and abnormal conditions such as offset and stuck resistance should be dealt with in time.

    During the operation, the operator shall not leave the post without authorization, and the load shall not be allowed to hang in the air for a long time.Rely on the limit switch to control the lifting limit, prevent accidents such as rushing to the top and taking off the rope, and avoid dangerous areas such as equipment clamping points during operation.

    Cart operation

    Before the cart starts, make sure that the whole line of the track is unobstructed, and the limit stop at the end of the track is intact, and investigate the personnel, vehicles and obstacles along the track.The operation process remains low-speed and stable, and decelerates in advance near the end of the track and in densely populated areas, and high-speed sprinting is prohibited.At the same time, pay attention to the deformation of the equipment caused by the track slope and load, and adjust the operating speed in a timely manner to prevent derailment and collision accidents.

    Trolley operation

    When the trolley is moving, maintain a sufficient safe distance from the end of the main beam and other equipment to prevent collision.Try to avoid operations such as emergency stops, sharp turns, and rapid movement as much as possible to reduce the load and swing significantly.When the cart and trolley need to work together, the two movements cooperate smoothly and run at a uniform speed, and the trajectory and attitude of the crane are continuously paid attention to throughout the process, so as to eliminate safety hazards in a timely manner.

    Operator Safety and Training Requirements

    Bridge cranes are special equipment. Only authorized personnel who are licensed and professionally trained can operate the equipment. It is strictly forbidden to start operations without witnesses and personnel who have not been assessed.

    Operators must fully master the core knowledge and practical skills of the equipment, including: equipment rated load parameters, load chart interpretation, equipment control logic, fault emergency response process, standardized command signals, equipment inspection specifications, safe hoisting and bundling technology, on-site risk identification and prevention and control methods.

    Enterprises need to establish a normalized training mechanism. After safety accidents, dangerous situations, equipment transformation, and long-term downtime and reuse, they must organize retraining and assessment to ensure that the skills of operators meet the standards.

    At the same time, the operators are given the right to stop work safely. When the equipment is abnormal or the site is unsafe, the operation can be stopped immediately to prevent risky construction in violation of regulations.All operators must strictly abide by local special equipment safety regulations, hold a certificate to take up the post, and review on time.

    Regular Inspection and Preventive Maintenance

    The core of the long-term safe operation of equipment lies in “prevention as the main and prevention as the combination”. It is necessary to strictly follow the original equipment specifications, ASME B30.2 industry standards and national special equipment management requirements, and formulate hierarchical inspection and maintenance plans according to the frequency of equipment use and operating load.

    • Daily pre-shift inspection: complete visual inspection and functional testing before each shift starts, focusing on verifying the main structure, wire rope, hook, brake, limit, emergency stop device, control system and operating environment, test safety warning devices and keep inspection records.
    • Periodic in-depth inspections: in-depth inspections are carried out on a monthly, quarterly, and annual basis, including structural nondestructive testing, electrical system testing, wear inspection of transmission and hoist components, track calibration, safety protection device verification, synchronous lubrication debugging, and load testing of heavy-duty equipment as needed.
    • Inspection and maintenance file records: establish an equipment ledger, register inspection results, hidden dangers, rectification plans, replacement of accessories and running time.Rely on the ledger for predictive maintenance and replace aging parts in advance; perform locking and listing during maintenance to cut off power to ensure safety.

    What to Do When a Bridge Crane Problem Occurs

    Once abnormal conditions such as abnormal equipment noise, abnormal vibration, control failure, material offset, and component caton are found during the operation, the following procedures shall be handled strictly in accordance with the following procedures to prevent panic operations and illegal handling.:

    • Immediate shutdown: Once the equipment is found to be abnormal, all lifting operations will be stopped as soon as possible, and the control of the equipment will be terminated to prevent the failure from further expanding, and to avoid secondary safety accidents such as falling objects and collisions.
    • Safe blanking: If the hoisting material is in a floating state, under the premise of fully evaluating the safety, slowly and smoothly lower the load to the ground or a stable and reliable support position. It is not allowed to hang the material in the air for a long time, let alone leave without authorization when the hanging object is floating.
    • Equipment isolation: strictly abide by the safety management specifications of the factory, cut off the power supply of the equipment and implement the locking and listing (LOTO) process, isolate and protect the faulty crane, and strictly prohibit unrelated personnel from trying to start and test the equipment.
    • Report and prepare: report fault information to on-site management personnel and equipment maintenance departments in a timely manner, and clearly describe the phenomenon, equipment status and operating conditions at the time of the failure, so as to facilitate rapid judgment of the problem.
    • Re-inspection and reuse: Faulty equipment must be tested and repaired by professional maintenance personnel, and after passing the acceptance, it can be put back into lifting operations.At the same time, it is necessary to dig deep into the root cause of the failure and implement corresponding prevention plans to prevent similar failures from happening again.

    Common Bridge Crane Safety Mistakes to Avoid

    Most lifting safety accidents are caused by habitual illegal operations. The following high-frequency misunderstandings need to be resolutely avoided during operation.:

    • Overload operation: Ignoring the rated load limit of the bridge crane, blindly carrying out overload hoisting, overestimating the carrying capacity of the equipment, so that the equipment can withstand loads that exceed the design standards.
    • Illegal use of spreaders: the use of damaged, deformed, lack of rated load identification or non-standard specifications of spreaders and rigging, the safety performance of the spreader itself cannot be guaranteed.
    • Illegal hoisting operations: implement dangerous behaviors such as cable-stayed slanting, dragging heavy objects, and violently lifting and falling, which will form an impact load on the load, which can easily cause the spreader to break or the equipment to be damaged.
    • People standing under the crane: Tacitly allow personnel to stand, pass or operate under the floating crane. Once the load falls, it will directly cause serious personal injury.
    • Operation with faults: ignoring abnormal signals such as abnormal noise, abnormal vibration, slippage, and caton of equipment, and continuing to carry out lifting operations knowing that there are hidden dangers.
    • Destruction of safety devices: artificially shield, remove, short-connect safety protection devices such as limit switches and brakes, and remove the safety protection barriers of the equipment.
    • Illegal on-duty operations: operators are on-duty without a license, tired or distracted during operations, and operate the crane without receiving complete professional training.
    • Omit the pre-shift inspection: simplify or even skip the pre-shift safety inspection directly. The inspection work is perfunctory, resulting in missed inspection of equipment hidden dangers, and the risks cannot be investigated in advance.
    • Hanging objects are placed in the air: the materials are hung in the air for a long time after the operation is over, and the site is unattended, which greatly increases the safety risk of the load falling.
    • Forced operation with illness: After discovering that the equipment failed, it did not stop in time, and was lucky enough to continue to operate with illness, and forced to make do with the operation.
    • Lack of on-site management: The command and communication mechanism of the hoisting site is chaotic, and the safety isolation operation area is not delineated, which is prone to situations where unrelated personnel strayed into the dangerous area.
    • Lack of maintenance work: failure to comply with the equipment maintenance cycle, long-term failure to arrange inspections and repairs, failure to replace worn and aging parts in time, accelerate the aging and failure of equipment.

    How Crane Design Can Improve Workplace Safety

    The safety and security of modern bridge cranes not only rely on standardized operation and maintenance, but also rely on scientific equipment design to reduce the risk of accidents from the hardware level. The mainstream safety design configuration is as follows:

    • Matching selection of load and working conditions: In accordance with CMAA, FEM, and ISO related standards, cranes with rated load and working level adapted to on-site working conditions are selected to meet the needs of different working loads.
    • Multiple load safety protection: equipped with dual braking system, overload protection and load monitoring device to effectively prevent dangerous situations such as overload and car slip.
    • Travel limit protection device: configure the upper and lower lifting limits, operating limits, and anti-collision devices to avoid accidents caused by over-range operations from the hardware level.
    • Multi-point emergency stop system: Set up a multi-point emergency stop mechanism, which can quickly cut off the power source of the equipment, and realize shutdown and risk avoidance in emergency situations.
    • Frequency conversion drive control system: equipped with a frequency conversion drive system, it realizes smooth start-stop and uniform speed operation, which significantly reduces the load swing during hoisting.
    • Diversified control methods: equipped with a handheld operation box and a wireless remote control device to optimize the standing position of the operator and reduce the safety risks caused by blind spots in the field of vision.
    • Sound and light early warning device: standard warning lights and sound and light alarms are equipped to continuously issue safety warnings during the operation of the crane and actively warn of risks.
    • Multi-machine anti-collision protection: In scenarios where multiple cranes work together on the same track, an anti-collision system is installed to avoid collisions between equipment.
    • Track end protection structure: strengthen the track end buffer and limit stop to enhance the overall stability of the cart during operation.
    • Automated auxiliary system: For repetitive hoisting operations, automatic positioning and anti-swing system are optional to reduce human operation errors.
    • Optimized design of structure and maintenance: adopt an anticorrosive and wear-resistant structure design, and reserve a channel for convenient inspection and maintenance to facilitate daily investigation of hidden dangers.

    Conclusion

    Bridge crane safety management is a system engineering that includes equipment design, installation, inspection, operation, training, maintenance and emergency management.Enterprises need to comply with OSHA 1910.179, ASME B30 and local special equipment regulations, implement pre-shift inspections, licensed induction, regular maintenance and investigation of hidden dangers, and formulate safety operating procedures based on working conditions.

    Take into account risk prevention and standardized operation during operation, rely on various safety protection devices to reduce risks, and carry out personnel training and emergency drills.Henan Mine Crane can provide safety configuration and technical support for bridge cranes based on plant conditions, loads, operating frequencies and environments, and assist enterprises in building safety operation and maintenance plans adapted to the site.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Match Crane Capacity with Factory Floor Load Limitations

    How to Match Crane Capacity with Factory Floor Load Limitations

    How to Match Crane Capacity with Factory Floor Load Limitations

    In industrial production, cranes are the core equipment of material handling, and the rationality of their selection directly affects production efficiency and plant safety.When many companies buy cranes, they often only pay attention to the lifting weight, but ignore the carrying restrictions on the ground of the plant, which eventually leads to the inability of the equipment to be installed, the ground cracking and even production stagnation.This article will explain in detail how to accurately match the crane capacity and the ground carrying capacity of the plant from a professional perspective, so as to help enterprises avoid the misunderstanding of selection and achieve safe, efficient and economical equipment configuration.

    Crane Capacity and Floor Load Requirements

    The ground carrying capacity of the plant is the core prerequisite for determining the feasibility of crane installation, and it is also the primary consideration for selection.There are significant differences in the carrying requirements of cranes of different tonnages and structural forms on the ground of the plant.For example, Henan Mine Crane manufactured light single-girder cranes have relatively low ground carrying requirements, while heavy double-girder cranes, gantry cranes, etc., due to their large weight and the concentration of loads generated during operation, the requirements for the strength, thickness and base structure of ground concrete are more stringent.If the ground carrying capacity is insufficient, even if the performance of the crane itself is up to standard, it will not be able to be installed and used safely, and it will even cause safety hazards such as ground settlement and cracking, which will affect the overall structural safety of the plant.

    Many companies have a cognitive misunderstanding that equates the rated lifting weight of the crane with the actual weight of the plant, which is extremely dangerous.In fact, when the crane is running, the actual load on the ground of the plant is much larger than the rated lifting weight. It is necessary to consider the crane’s own weight, lifting weight, and additional loads generated during operation.Among them, additional loads include inertial forces during starting and braking, vibration loads in operation, etc. These dynamic loads will instantly increase the force and pressure on the ground.If the ground carrying demand is estimated only according to the lifting weight, it can easily cause the actual load to exceed the ground’s bearing range and cause a safety accident.

    How to Determine the Right Crane Capacity for a Factory

    Analyze material handling requirements

    The first step in determining the crane capacity is to comprehensively analyze the material handling needs of the enterprise.First of all, it is necessary to clarify the maximum material weight that needs to be hoisted in the production process, as the core reference for the basic capacity of the crane, and at the same time reserve a safety margin of 10%-20% to avoid long-term full-load operation affecting equipment life and safety.Secondly, the production frequency should be considered. If the material handling frequency is high and the operation intensity is high, it is necessary to choose a crane model adapted to high-frequency operation to avoid production efficiency degradation due to insufficient capacity.In addition, it is necessary to combine the company’s future production expansion plans to reserve a certain amount of capacity space to avoid the replacement of equipment due to increased production capacity in the later stage and increase investment costs.

    Calculate total crane load

    Accurate calculation of the total load of Henan Mine Crane manufactured crane is the key link to match the ground load.The total load includes not only the lifting load, but also the self-weight of all components such as crane bridges, trolleys, wire ropes, hooks, etc. These self-weight loads are the main static loads borne by the ground.At the same time, the influence of dynamic loads must be considered. During the operation of the crane such as starting, braking, and luffing, inertial forces and vibration loads will be generated, which usually need to be estimated at 1.2-1.5 times the static load. The specific coefficient needs to be determined according to the working level and operating conditions of the crane.Only by comprehensively calculating static and dynamic loads can the carrying capacity required by the ground be accurately judged.

    Consider crane duty class and operating conditions

    The working level and actual operating conditions of the crane directly affect the rationality of the structural strength and capacity configuration of the equipment.There are differences in the design life, load cycle times and operating strength of cranes of different working levels. The higher the working level, the more stringent the requirements for the structural strength and carrying capacity of the equipment.For example, A6-A8-level high-work-level cranes are suitable for high-frequency and high-intensity operation scenarios. Their structural design needs to consider greater load impact, and the corresponding ground carrying requirements are also higher.Therefore, when determining the crane capacity, it is necessary to combine the actual operating frequency, load characteristics, and environmental conditions (such as high temperature, humidity, dust, etc.) to select the appropriate working level to ensure that the equipment matches the ground carrying capacity.

    How to Evaluate Factory Floor Load Limitations

    Check existing floor structure

    To evaluate the ground carrying restrictions of the plant, we must first verify the structural parameters and carrying data of the existing ground.You can obtain core information such as the strength level, thickness, and steel bar configuration of the ground concrete by consulting the design drawings and completion materials of the plant, and at the same time confirm the treatment method and carrying capacity of the ground base layer.If relevant information is lacking, it is necessary to entrust a professional organization to conduct on-site testing, through concrete strength testing, grass-roots bearing capacity testing, etc., to clarify the actual carrying limit of the ground.For old factories, it is also necessary to focus on checking the ground for cracking, sedimentation, sanding and other problems, assess the integrity of the ground structure, and avoid insufficient carrying capacity due to the aging of the ground.

    Calculate maximum wheel load

    When the crane is running, the maximum pressure generated by a single wheel is a key indicator to evaluate the carrying capacity of the ground, which directly determines whether the ground can withstand concentrated loads for a long time.When calculating the maximum wheel pressure, it is necessary to combine the total load of the crane, the number of wheels, the wheel track and other parameters, consider the load distribution of the crane at different operating positions (such as the midpoint and end of the span), and find out the maximum wheel pressure value.At the same time, the influence of dynamic load needs to be considered, and the calculation results should be appropriately enlarged to ensure that the ground carrying capacity can meet the long-term effects of maximum wheel pressure.If the maximum wheel pressure exceeds the ground carrying limit, ground reinforcement measures or crane selection adjustments need to be taken.

    Consider load distribution factors

    The span, wheel track and operating position of the crane will directly affect the distribution of the load on the ground, which in turn affects the carrying pressure of the local area.Reasonable span and wheel track design can evenly distribute the load to the ground and reduce the carrying load in the local area. During the operation of the crane, the load will shift with the change of position. If the load in the local area is concentrated, it can easily lead to ground load overrun.Therefore, when evaluating the ground load-bearing limit, it is necessary to combine the structural parameters of the Henan Mine Crane manufactured crane to analyze the load distribution law, and focus on the carrying capacity of the load concentration areas such as under the track and around the column to avoid local overload problems.

    Matching Crane Capacity with Factory Floor Conditions

    Select crane type based on structural limitations

    There are obvious differences in the requirements of different types of cranes for the ground carrying of the plant. According to the structural conditions and carrying restrictions of the plant, the appropriate crane type needs to be selected.For example, single-girder cranes have lighter weight and lower requirements for ground carrying. They are suitable for factories with limited ground carrying capacity and small spans. Double-girder cranes have strong carrying capacity and are suitable for heavy material handling, but they have higher requirements for ground carrying. Gantry cranes are suitable for open-air or large-span scenarios in factories, and their ground carrying requirements need to be determined in combination with specific models and parameters.In addition, it is necessary to consider the space height, column spacing and other conditions of the plant to ensure that the crane can operate normally after installation without affecting the layout of other equipment in the plant.

    customized crane solution

    Optimize crane design to reduce floor pressure

    Under the premise of determining the crane capacity, the equipment design can be optimized to reduce the pressure on the ground and achieve accurate matching with the ground carrying capacity.For example, the use of lightweight design concept, the selection of high-strength, lightweight materials, reduce the weight of the crane itself, thereby reducing the total load, optimize the structural parameters of the crane, such as reasonable adjustment of the wheel track, increase the number of wheels, disperse the wheel pressure, reduce the maximum wheel pressure of a single wheel, the use of advanced shock absorption technology, reduce the vibration load during the operation of the crane, reduce the impact of dynamic loads on the ground.These optimization measures can effectively relieve the ground carrying pressure without affecting the performance of the crane.

    Balance capacity, performance, and cost

    When matching the crane capacity and ground carrying conditions, it is necessary to take into account the balance of capacity, performance and cost.On the one hand, it is necessary to avoid insufficient capacity leading to low production efficiency and inability to meet material handling needs. On the other hand, it is necessary to avoid blindly pursuing high capacity, which will lead to increased equipment investment and increase the burden on the ground. , And even need to invest in additional ground reinforcement costs.The crane plan with the highest price ratio should be selected based on the actual production needs of the enterprise and the ground carrying capacity. Under the premise of ensuring the safe and efficient operation of the equipment, the investment cost should be controlled and the economic benefits should be maximized.

    Common Mistakes When Matching Crane Capacity with Floor Load Limits

    Ignoring total crane weight

    This is the most common misunderstanding in the selection of cranes by enterprises, that is, they only pay attention to the lifting weight and ignore the impact of the crane’s own weight on the ground load.Many companies believe that as long as the ground can withstand the lifting load, they can install a crane corresponding to the lifting weight, but they don’t know that the crane’s own weight often accounts for a large proportion of the total load. Coupled with the dynamic load, the actual ground force far exceeds expectations.This kind of incorrect estimation method can easily lead to ground load-bearing overruns, causing safety hazards such as ground cracking and equipment tilting, and the cost of late rectification is extremely high.

    Installing high-capacity cranes in weak structures

    In order to reserve future production needs, some enterprises blindly choose high-capacity cranes, but did not conduct a comprehensive assessment of the ground carrying capacity of the plant, and installed high-capacity cranes on the ground with weak carrying capacity.This approach will not only cause the equipment to fail to operate normally, but also cause irreversible damage to the plant structure and even cause safety accidents.If the problem of insufficient carrying capacity is to be solved in the later stage, large-scale reinforcement of the ground is required, which will not only affect the production schedule, but also increase additional investment costs, and the gains will not outweigh the losses.

    Best Practices for Crane Capacity Selection

    Conduct professional load assessment

    Before installing the Henan Mine Crane manufactured crane, it is necessary to carry out professional load assessment work, combined with the production needs of the enterprise and the ground conditions of the plant, to conduct a comprehensive and accurate analysis.You can entrust a professional crane manufacturer or a third-party testing agency to conduct on-site testing of the ground carrying capacity, calculate the total crane load, maximum wheel pressure and other key parameters, and evaluate the matching between the ground and the crane.Through professional evaluation, potential problems can be identified in advance, reasonable selection plans and ground reinforcement measures can be formulated to ensure the safe and stable operation of the crane after installation.

    Choose a customized crane solution

    There are differences in the production needs and plant conditions of different enterprises, and it is often difficult for standardized crane products to fully match the actual needs.Therefore, it is recommended to choose a customized crane solution, and the professional manufacturer will tailor the capacity, structure and configuration of the crane according to the company’s material handling needs, ground carrying restrictions, plant space and other parameters.The customized solution can accurately match the ground carrying conditions, avoid waste of resources and safety hazards, and ensure that the performance of the crane can meet production needs and achieve efficient and safe material handling operations.

    Henan Mine Crane Factory Custom

    Accurately matching the crane capacity and the ground carrying limit of the plant is the core link of crane selection, which is directly related to production safety, efficiency and cost.In the selection process, enterprises need to abandon cognitive misunderstandings, comprehensively analyze the ground carrying conditions and production requirements, and select the most suitable crane solution through the professional evaluation and customized design of Henan Mine Crane Factory to achieve the perfect adaptation of equipment and plant, and escort the efficient production of enterprises.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Maintain an Insulated Overhead Crane in Hazardous Areas

    How to Maintain an Insulated Overhead Crane in Hazardous Areas

    How to Maintain an Insulated Overhead Crane in Hazardous Areas

    An insulated overhead crane fails in a different way than a standard crane fails. The bridge doesn’t just wear out. It loses the dielectric barrier that keeps stray current from a live load out of the operator’s cab. In non-ferrous smelting plants, substations, and live-line maintenance bays, that barrier is the entire safety case for the equipment. Maintaining an insulated overhead crane in a hazardous area means protecting two separate risk systems at once: electrical insulation integrity and explosion or fire protection. This guide breaks down exactly how to do both, with the testing procedures, schedules, and compliance checks that keep the crane, and the people under it is safe.

    What Is an Insulated Overhead Crane?

    Henan Mine Crane Factory supply insulated overhead crane is a bridge crane built with dedicated insulation devices that block electrical current from traveling from a live load, through the hook and hoisting mechanism, into the crane structure and operator’s cabin. It is not the same thing as an explosion-proof crane, even though the two terms are routinely confused in industry content.

    Insulated cranes are purpose-built for environments where the load itself can carry current, non-ferrous metal smelting (electrolytic aluminum, zinc, lead, magnesium, copper), substations, power plants, and electrified railway maintenance. Insulation is typically layered at three critical points:

    • Between the hook and the movable pulley block
    • Between the hoisting mechanism and the trolley frame
    • Between the wheel sets/bearings and the rail or end carriage

    Explosion-proof (ATEX/IECEx) cranes solve a different problem: preventing sparks or surface heat from igniting flammable gas, vapor, or combustible dust in the surrounding atmosphere. A crane can be insulated, explosion-proof, both, or neither and many of the harshest real-world settings, like electrolytic aluminum cells running near 900°C with combustible carbon dust in the air, require both protections layered together.

    Why Hazardous Areas Demand Specialized Insulated Crane Maintenance

    Standard crane maintenance schedules are written for clean, climate-controlled facilities. Hazardous areas break that assumption in three ways that directly attack insulation integrity:

    • Heataccelerates the breakdown of insulating materials and coatings, and electrolytic workshops frequently run with cell temperatures near 900°C nearby.
    • Humidityabove roughly 85%, common in smelting halls, lowers surface resistance on insulators and creates leakage paths that a dry-environment inspection schedule would miss.
    • Conductive dust, carbon, graphite, or metal particulatecan bridge insulation gaps that were never designed to handle a contaminated, conductive coating.

    The stakes of getting this wrong are well documented. Crane-related incidents across U.S. industry have caused dozens of worker fatalities annually, and improperly certified or maintained equipment in hazardous zones has triggered multi-million-dollar regulatory penalties after near-miss incidents at chemical and processing sites. Maintenance isn’t a cost center here, It’s the control that keeps a known hazard from becoming an incident.

    Hazardous Area Classifications and What They Mean for Maintenance

    Before building a maintenance plan, you need to know which zone the crane operates in, because the classification dictates inspection rigor, intervals, and who is authorized to do the work.

    • Zone 0/20— explosive atmosphere present continuously or for long periods
    • Zone 1/21— likely to occur occasionally during normal operation
    • Zone 2/22— occurs rarely, only for short periods
    • The “G” suffix denotes gas/vapor atmospheres; “D” denotes combustible dust

    These zones are governed under ATEX (EU), IECEx (international), or GB standards (China), with electrical components rated accordingly. For example, an Ex de IIB/IIC T4 motor enclosure. For Henan Mine Crane Factory supply insulated cranes specifically, the relevant insulation design standard is typically referenced alongside the general crane standard (in China, GB/T 14405 alongside JB/T 10219 for explosion-proof/insulation requirements). The zone classification determines testing frequency: equipment in Zone 1 or in continuously humid/dusty conditions needs insulation checks every 3–6 months rather than the annual cycle acceptable for benign environments.

    Pre-Maintenance Safety Protocol: Lockout, Isolation, and Area Clearance

    Before any tool touches the crane, the area and the power supply both need to be secured. OSHA’s crane maintenance procedure (29 CFR 1910.179) lays out the baseline sequence, and it applies directly to insulated and hazardous-area cranes:

    1. Move the crane to a position that minimizes interference with other cranes and operations.
    2. Place all controllers in the off position.
    3. Open and lock the main or emergency power switch. This is the lockout/tagout (LOTO) step.
    4. Post warning or “out of order” signs on the crane, and visibly on the floor or hook below.
    5. If other cranes share the runway, install rail stops or equivalent barriers to prevent interference with the idled unit.
    6. Do not return the crane to service until all guards are reinstalled, safety devices are reactivated, and maintenance equipment is cleared.

    In a hazardous area, add a gas/dust atmosphere check and confirm hot work or spark-producing tools are permitted under the site’s permit system before proceeding.

    Insulation Resistance Testing: The Core Maintenance Task

    This is the test that’s unique to Henan Mine Crane manufactured insulated crane maintenance, and it’s the one most generic crane maintenance checklists omit entirely.

    Insulation resistance testing (often called a “megger test”) applies a DC test voltage across an insulating device and measures the leakage current that escapes, converting it to a resistance value in megohms via Ohm’s Law. Lower resistance means a more degraded insulation barrier.

    Key parameters to follow:

    • Test voltage: 500V or 1,000V DC is standard for routine maintenance testing; higher voltages (2,500V–5,000V) are reserved for stress-testing healthy insulation, not routine field checks.
    • Minimum acceptable resistance: insulated crane devices (hook-to-pulley, hoist-to-trolley, wheel-to-rail insulation) are commonly specified to exceed 0.5 megohm total under crane-specific design standards. Motors and cables follow the broader industry guideline of roughly 1 megohm per kV of operating voltage as a baseline, compared against manufacturer specs and prior readings, not treated as an absolute pass/fail line.
    • Spot reading method: apply the test voltage and take the resistance reading after one minute to let capacitive charging current stabilize.
    • Polarization index: for motors and larger insulation systems, compare the 1-minute and 10-minute readings; a ratio below 1.0 signals contaminated or deteriorating insulation.
    • Frequency: annually for equipment in benign conditions; every 3–6 months for equipment exposed to heat, humidity, dust, or chemical contamination, which describes most hazardous-area smelting and processing environments.
    • VFD caution: always disconnect motors from variable frequency drives before testing; the test voltage can damage drive electronics.

    Record every reading against the equipment’s history. A sudden drop between tests is a more urgent signal than any single absolute number.

    Insulated Overhead Crane

    Inspecting Electrical Components, Wiring, and Conductor Rails

    Having finished the insulation testing, go to a comprehensive visual and functional inspection of the electrical system, that is:

    • Motors and terminals: look out for corrosion, cracked enclosures or any wear on insulation that might allow dangerous gas or dust to enter internal compartments.
    • Conductor rails, cable trolleys:check for mechanical damage, heat damage, chemical attack on insulated sections of conductor rails and cable insulation.
    • Control cabinets: ensure the intactness of the insulating isolation devices situated between the control circuits and the containing cabinet, also equipped watertight/dust-tight seals on enclosures adopted IP55 or higher.
    • Grounding continuity: The crane bridge frame must be continuous and grounded all the way from the path to the operator‘s cabin, the cabin must be bonded to the bridge so the condition for the operator‘s station is maintained.
    • Explosion-proof enclosures (if dual-rated):make sure flameproof joint surfaces are free of cracks, corrosion or gaps, which could jeopardize the Ex rating.

    Photograph each of your findings and document torque and/or resistance readings where appropriate. This will be useful for the compliance step later.

    Mechanical and Structural Checks

    Insulation depends on mechanical integrity as much as electrical integrity, since a damaged insulating pad or bearing housing is a direct path to current leakage:

    • Insulated wheel sets and bearings: inspect for cracking, glazing, or compression of the insulating material itself, not just normal mechanical wear.
    • Hoist ropes and load chains: check for heat damage, corrosion, and wire breaks, especially where ropes pass near high-temperature processes.
    • Brakes: confirm fail-safe disc brakes apply instantly on power loss; in high-heat environments, verify linings haven’t degraded from thermal exposure.
    • Gearboxes: check oil bath seals; in dusty environments, contamination of gear oil is an early warning sign of seal failure.
    • Structural steel and insulating coatings: inspect welds (per applicable grade standards) and confirm the insulating coating layer over the steel hasn’t been abraded down to bare metal at contact points.

    Lubrication Practices for Hazardous, High-Heat Environments

    Standard grease schedules don’t transfer directly to hazardous areas:

    • Use high-temperature lubricantsrated for the actual operating range, some hazardous-area applications swing from -40°C to over 200°C, and a lubricant rated for only one end of that range will fail at the other.
    • In combustible-dust or cleanroom-adjacent environments, use non-volatile, low-residue lubricants, and consider oil-free, dry-lubrication guide rails where contamination from leaking grease is itself a hazard.
    • Adjust viscosity seasonally if the facility experiences large ambient temperature swings.
    • Never use a lubricant that hasn’t been checked for compatibility with the insulating materials it will contact, some greases are mildly conductive and can compromise an otherwise intact insulation barrier.

    Building a Preventive Maintenance Schedule

    A written, zone-aware schedule is what turns these checks into a repeatable program rather than a reactive one.

    Interval Tasks
    Daily/Pre-shift Visual check of warning systems, hook/load chain condition, brake function, signage
    Monthly Corrosion check on load-bearing joints and insulating coatings; lubrication top-off; conductor rail visual inspection
    Quarterly (harsh zones) Insulation resistance spot test on all insulation devices; control cabinet seal check
    Annually Full insulation resistance test with polarization index; explosion-proof enclosure certification check; structural inspection per OSHA 1910.179; gearbox oil analysis
    Per regulatory cycle ATEX/IECEx/GB certification renewal and documentation audit

    Adjust the quarterly and monthly cadence upward for any crane operating continuously in Zone 1 conditions or in cells running above roughly 80% humidity.

    Common Failure Points and How to Prevent Them

    A handful of failure modes account for most insulated-crane maintenance incidents:

    1. Conductive dust bridging an insulation gap: prevent with sealed motor/gearbox housings rated IP65 or higher and more frequent cleaning cycles.
    2. Insulation degradation from sustained heat exposure: prevent with scheduled resistance testing rather than relying on visual inspection alone, since heat damage is often invisible until failure.
    3. Grounding discontinuity between cabin and bridge: prevent with a dedicated bonding check at every annual inspection, not just at commissioning.
    4. Lubricant contamination acting as a conductive or fuel path: prevent with lubricant compatibility checks and IP-rated seals.
    5. Mixing insulated-crane assumptions with explosion-proof requirements: prevent by maintaining separate checklists for each protection system, since a crane can pass an insulation test while having a degraded Ex enclosure, or vice versa.

    Compliance, Documentation, and Certification Renewal

    Hazardous-area crane operation is a regulated activity, and the maintenance record is the evidence of compliance:

    • Maintain detailed electrical documentation covering grounding, wiring, and cable routing against the applicable standard (ATEX, IECEx, or GB).
    • Keep insulation resistance test logs with dates, readings, and the instrument usedauditors and insurers will ask for trend data, not just a single pass/fail result.
    • Track certification expiry separately from maintenance intervals.A Henan Mine Crane manufactured crane can be mechanically sound and still be out of regulatory compliance if its Ex or insulation certification has lapsed.
    • Train and document qualification of every technician who performs insulation testing or works on explosion-proof components. This is typically a named requirement under both OSHA and ATEX/IECEx frameworks.

    Regulators in the EU and elsewhere have issued multi-million-euro penalties following hazardous-area equipment failures tied to certification gaps, underscoring that documentation is not a paperwork formality. It’s the audit trail that protects both workers and the business.

    Frequently Asked Questions

    Q: What’s the difference between an insulated overhead crane and an explosion-proof crane?

    An insulated overhead crane blocks electrical current from a live load reaching the operator and structure, using insulation at the hook, hoist, and wheel assemblies. An explosion-proof crane prevents sparks or excess heat from igniting flammable gas, vapor, or dust in the surrounding atmosphere. They address different hazards and are certified under different standards, though a single crane can carry both protections.

    Q: How often should insulation resistance be tested on a hazardous-area crane? Annually is the baseline for benign conditions, but cranes operating in heat, humidity above roughly 85%, or dust-heavy zones should be tested every 3 to 6 months. Frequency should always be tightened, not relaxed, if a previous reading showed a meaningful drop from baseline.

    Q: What is the minimum acceptable insulation resistance for an overhead crane? Crane-specific insulation devices are commonly held to a minimum of 0.5 megohm under dedicated crane insulation standards, while motors and cables are typically benchmarked against roughly 1 megohm per kV of operating voltage. The more important signal is a sudden drop from the equipment’s own historical readings rather than any single absolute threshold.

    Q: Can an insulated crane also be explosion-proof?

    Yes. Environments like electrolytic aluminum smelting combine high current, heat, humidity, and combustible carbon dust, so the crane needs insulation devices and explosion-proof electrical components rated for the applicable gas/dust zone simultaneously. These are maintained as two separate checklists run on the same machine.

    Q: What lubricants are safe to use on cranes in combustible dust environments? Use high-temperature, low-residue lubricants rated for the facility’s actual temperature range, and avoid any grease that hasn’t been checked for electrical conductivity if it will contact insulated components. In contamination-sensitive zones, oil-free or dry-lubrication guide rail systems reduce the risk of leaked grease creating either a fire-fuel source or a conductive bridge.

    Q: Who is qualified to perform insulated crane maintenance in a hazardous area? Maintenance and insulation resistance testing should only be performed by personnel trained and documented as qualified under the site’s electrical safety program, with specific competency in hazardous-area work (ATEX/IECEx-recognized training where applicable). This qualification requirement is typically enforced under both general crane safety regulations and hazardous-area equipment directives.

    Henan Mine Crane Factory Custom

    Maintaining an insulated overhead crane in a hazardous area isn’t a single checklist. It’s two protection systems, electrical insulation and explosion/fire safety, run in parallel on the same equipment. Start with a clear zone classification, build insulation resistance testing into a frequency that matches the actual environment , and keep mechanical, lubrication, and documentation practices aligned to both hazard types. Get those four pieces right and the crane will keep doing what it’s there for: moving a dangerous load safely, every time.

    When reliability, compliance, and safety can’t be compromised, Henan Mine Crane provides fully customized insulated and explosion-proof overhead crane solutions built for real industrial conditions. From engineering design to on-site application support, Henan Mine Crane Factory help facilities optimize safety performance, reduce downtime risk, and ensure long-term stable operation in the most demanding hazardous environments.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Install Heavy Duty Gantry Cranes in Existing Steel Structure Workshops

    How to Install Heavy Duty Gantry Cranes in Existing Steel Structure Workshops

    How to Install Heavy Duty Gantry Cranes in Existing Steel Structure Workshops

    Heavy-duty gantry cranes are widely used in manufacturing, warehousing and heavy industry processing scenarios, and undertake large-scale material hoisting, transshipment and assembly operations.In the stage of upgrading production capacity, many enterprises hope to use the built steel structure workshop to install lifting equipment to avoid the high cost and long construction period of the new plant.Heavy-duty gantry cranes have a large impact on their own weight and dynamic load, and have strict requirements for the bearing capacity, ground load, space clearance and foundation foundation of the steel structure of the original plant. Direct construction without evaluation can easily cause hidden dangers such as component deformation, ground settlement, and equipment stagnation, and even fail to pass safety acceptance.The installation of the plant needs to evaluate the adaptability of the site first, implement pre-testing, targeted structural transformation, standardized installation and load acceptance, while taking into account the project cost and production shutdown control, and provide a complete landing idea for the workshop hoisting transformation.

    Can a Heavy-Duty Gantry Crane Be Installed in an Existing Workshop?

    The core issue that many factory managers are most concerned about is whether the built steel structure plant can be equipped with heavy gantry cranes?The answer is yes, but the three core conditions of structure, load, and space must be met. Not all factories are suitable.Light-duty gantry cranes can be easily installed, while heavy-duty gantry cranes with a rated lifting weight of more than 5 tons need to be specially evaluated in combination with the original parameters of the plant and the working conditions of the equipment. Factories that do not meet the conditions must be retrofitted before installation, and direct construction is strictly prohibited.The following are the three core adaptation evaluation dimensions.

    Workshop structure assessment

    The stability of the steel structure of the plant is the basic prerequisite for the installation of heavy gantry cranes.The specifications and materials of the steel columns, steel beams, roof supports, inter-column supports, and connecting bolts of the existing steel structure plant directly determine whether it can carry the static load, dynamic load, and braking impact force generated by the operation of the gantry crane.First of all, it is necessary to verify the original construction drawings of the plant and confirm the load-bearing parameters of the steel structure design, the cross-section dimensions of the components, and the steel labels.Secondly, investigate the current situation on the site, whether there are aging and damage problems such as steel column corrosion, steel beam deformation, weld cracking, loose bolts, and missing support.

    At the same time, it is necessary to distinguish the design and use of the plant. Most of the ordinary light-duty processing and storage steel structure plants do not reserve lifting equipment loads, and the overall stiffness and side resistance are insufficient, which cannot be directly adapted to heavy gantry cranes.The heavy industry adapted steel structure plant has reserved the lifting load margin, which can be installed with a simple review.Professional engineers need to pass the structural force calculation and bearing capacity verification, and issue a plant structure evaluation report to determine whether the original steel structure meets the operating requirements of the equipment, and clarify whether it needs to be reinforced and transformed.

    Crane load requirements

    The load parameters of Henan Mine Crane manufactured heavy gantry crane are the core basis for the adaptation of the plant. The core includes three categories: static load, dynamic load, and impact load, which are indispensable.Static load refers to the fixed weight of the gantry crane, hook, trolley, wire rope, etc., and is the basic load-bearing pressure of the plant and the ground.Dynamic load is the alternating load generated when the equipment is running, the material is lifted and lowered, and the horizontal movement is made.The impact load is the instantaneous impact force generated at the moment of start, stop and braking, and it is also the key load that steel structures are most vulnerable to damage.

    The loads of heavy gantry cranes of different tonnages vary greatly, and the requirements of 10-ton, 20-ton, and 50-ton heavy equipment for the steel column force, ground load-bearing, and track foundation of the plant are completely different.In the evaluation stage, it is necessary to clarify the rated lifting weight, maximum operating span, lifting height, operating speed, and working level of the equipment, and calculate the overall carrying margin in combination with the plant structure to ensure that the ultimate carrying capacity of the plant > the total load of the equipment + the safety redundancy coefficient, so as to eliminate the risk of structural fatigue, deformation and collapse in long-term operation.

    Available installation space

    The space size is not up to standard, and no matter how qualified the structure is, the installation and normal operation of the gantry crane cannot be completed.First, verify the vertical clearance. It is necessary to meet the height of the gantry crane legs, the installation height of the main beam, and the maximum lifting height of the material. At the same time, reserve the top safety maintenance gap to avoid the collision of materials and equipment with the roof and steel beams of the plant.Secondly, check the horizontal span. The column spacing and overall span of the plant need to match the design span of the gantry crane to ensure that the equipment walks unobstructed and interference-free.

    At the same time, it is necessary to reserve equipment operation channels and maintenance space. There cannot be fixed equipment, shelves, or walls on both sides of the plant to block the walking track, and a buffer safe distance needs to be reserved at both ends to meet the needs of gantry crane limit braking, maintenance and maintenance.In addition, it is necessary to verify the space of the import, export and internal passages of the factory area to ensure the entry of large-scale component transportation and hoisting equipment, so as to avoid the construction problems that the equipment cannot enter and the installation space is insufficient.

    What Should Be Checked Before Gantry Crane Installation?

    After the plant adaptation assessment is passed, a full range of pre-verification must be completed before the formal construction. This is the key link to avoid installation failures, eliminate safety hazards, and ensure that the acceptance is qualified.Most of the problems of installation rework, equipment failure, and failure to pass safety supervision are due to omissions in the early verification.This link will clarify the main points of standardized verification from the three dimensions of building foundation, ground load, and operating environment.

    Building structure and foundation

    The main structure and foundation of the plant building are the core foundations for carrying heavy gantry cranes, and the verification work needs to be detailed and comprehensive.For building structures, it is necessary to review the verticality of the steel column, the flatness of the steel beam, and the firmness of the connection nodes of the steel structure twice, investigate weld defects, bolt fastening conditions, and the integrity of the support system, and confirm that the structure has no deformation, no loosening, and no aging damage.The key points of foundation foundation verification are foundation settlement, concrete strength, and foundation size.The long-term reciprocating operation of heavy-duty gantry cranes has extremely high requirements for foundation stability. It is necessary to test the concrete marking of the ground foundation of the plant to confirm whether it meets the equipment pressure standard.Investigate whether there are uneven settlement, cracking, and empty drum problems in the foundation. If the foundation sinks and the strength is insufficient, serious problems such as track deformation, equipment deviation, and structural tilt will occur in the later stage.All basic data must be kept in inspection records as the core information for subsequent acceptance and annual inspection.

    Floor load capacity

    The load-bearing capacity of the ground is an easily overlooked but vital verification item.Unlike ordinary equipment, Henan Mine Crane manufactured heavy gantry crane when walking, the load will be concentrated on the ground in the track paving area, and the local pressure is extremely high.It is necessary to accurately detect the load-bearing per unit area of the plant floor, the thickness of the concrete, and the flatness of the ground, and confirm that the ground can withstand the combined load of the gantry crane’s own weight and the maximum hoisting material.The ground of an ordinary factory building is only suitable for the passage of personnel and small equipment. It is not designed for centralized heavy-duty, and the gantry crane is directly installed on the track. Problems such as ground cracking, collapse, and track tilt will directly cause the equipment to fail to operate smoothly, greatly increasing the probability of safety accidents.If the ground load is not up to standard, targeted ground thickening, reinforcement of steel bars, and reinforcement of cushions are required to ensure that the ground carrying capacity meets the long-term operating standards of the equipment.

    Clearance and access conditions

    The verification of headroom and access conditions directly determines the efficiency of installation and construction and the safety of the equipment in the later stage of operation.Clearance verification needs to fully cover the operating area, reserve a safe height at the top, a horizontal clearance distance on both sides, and a buffer distance at the end, and completely remove obstacles such as pipelines, lamps, shelves, and temporary facilities within the operating range to ensure that the gantry crane does not interfere in the whole process of lifting, walking, and braking.The installation and passage conditions are mainly for the construction phase. It is necessary to confirm the entry route of heavy components such as large-scale hoisting equipment, gantry crane main beams, and outriggers, clean up obstacles in the factory area, level the entry road, and ensure the smooth entry of transportation vehicles and cranes. In place.At the same time, plan the construction site enclosure, work area, and safety warning area, do a good job of construction isolation, avoid cross-operation interference, and lay the foundation for safe and efficient construction.

    How to Modify an Existing Workshop for a Gantry Crane?

    Most old and ordinary steel structure factories cannot directly install heavy-duty gantry cranes, so targeted special retrofits need to be made based on the results of preliminary testing and evaluation.The renovation of the plant follows the principles of minimum changes, maximum safety, and optimal cost. There is no need for overall reconstruction. Only the reinforcement and optimization of weak links can meet the installation and operation standards of heavy gantry cranes.The core transformation is divided into three modules.

    Reinforcing the steel structure

    Steel structure reinforcement is the core process of plant transformation, and it is optimized for steel components with insufficient bearing capacity, insufficient stiffness, and poor stability.Common reinforcement methods include thickening and strengthening of steel beams and steel columns, adding inter-column support, roof transverse support, and oblique support components to enhance the overall steel structure’s resistance to lateral force and deformation, and offset the alternating load and impact force generated by the operation of the gantry crane.For steel components with corrosion, thin walls, and seriously insufficient bearing capacity, the corresponding specifications of high-strength steel need to be replaced. All reinforced welds are fully welded and fastened with high-strength bolts. After the welding is completed, anti-corrosion and anti-rust treatment will be done to avoid corrosion and aging of the components in the later stage.After the reinforcement is completed, the bearing capacity verification needs to be done again to confirm that the steel structure as a whole meets the load requirements of the long-term operation of the heavy gantry crane, and a reinforcement acceptance report is issued.

    Preparing the crane travel area

    The transformation of the walking area of the gantry crane directly affects the smooth operation and service life of the equipment.First, the ground and foundation of the walking track area are hardened and strengthened, the concrete cushion is thickened, and a double-layer steel mesh is added to enhance the overall pressure bearing capacity of the ground and prevent the ground from settling and cracking due to long-term heavy-duty operation.Secondly, accurately level the operating ground, control the ground flatness error within the industry standard range, and prevent the height difference after the track is paved.Accurately lay the line according to the design parameters of the gantry crane, determine the centerline of the track, pavement spacing, and elevation parameters, lay a special lifting track, and fix the track pressure plate, buffer baffle, and grounding device to ensure that the track parallelism, flatness, and spacing are fully up to standard.At the same time, clean up all debris and raised obstacles in the walking area, and polish the raised parts of the ground to ensure that the gantry crane walks smoothly, without caton, and without deviation.

    heavy-duty gantry crane installation

    Adjusting workshop clearance

    In view of the lack of headroom and space interference in the plant, refined space adjustments are required.For scenes where the top clearance is insufficient, the roof ancillary facilities can be optimized, the ceiling pipelines can be shifted, and the position of lamps and lanterns can be adjusted to maximize the use of vertical space.For situations where there is insufficient space on both sides, move the fixed equipment, shelves, and fixtures in the work area to broaden the walking space of the equipment.If there is a slight deviation in the span and column spacing of the plant, the installation and positioning of the gantry crane can be adjusted to adapt to the existing structure of the plant.If the spatial deviation is too large, the wall and column ancillary structures need to be partially modified to eliminate the risk of collision in equipment operation.After the transformation is completed, the headroom size will be reviewed in all directions to ensure that the lifting limit height, walking limit range, and maintenance operation space all comply with safety specifications.

    How Is a Heavy-Duty Gantry Crane Installed?

    After the preliminary verification and the acceptance of the plant renovation are passed, the standardized installation and construction of heavy gantry cranes can be started.Heavy-duty gantry crane components are large in size, heavy in weight, and require high installation accuracy,

    Component transportation and positioning

    Henan Mine Crane manufactured heavy-duty gantry cranes include main beams, outriggers, walking end beams, winches, trolleys, electrical systems and other large-scale components. Transportation and precise placement are the first step in installation.All components are packed in protective packaging before leaving the factory to avoid bumps, deformation, and corrosion during transportation. Special transportation vehicles are used for large, ultra-long and ultra-wide components, which are firmly fixed to prevent transportation displacement and damage to the equipment structure.After the components enter the field, they will be placed in partitions in accordance with the installation order, and the site will be leveled and cushioned. Sleepers and cushions will be placed under the heavy-duty components to avoid the components from directly touching the ground and being deformed by moisture.At the same time, combined with the construction drawings, precise placement and positioning, mark the installation point of the outrigger, the docking position of the main beam, and the track reference line, review all positioning dimensions, and provide accurate benchmarks for subsequent assembly and construction to eliminate installation deviations.

    Main girder and leg assembly

    The assembly of the main beam and outriggers is the core process of the entire installation project, which directly determines the overall stability and operating accuracy of the equipment.The construction adopts segmented hoisting and alignment assembly technology. First, a large crane is used to accurately lift the outriggers on both sides to a preset positioning point. After temporary fixation, the verticality and level are calibrated to ensure that the outriggers are not tilted or offset.Then the main bridge body is hoisted, the main beam is smoothly buttoned to the flange interface of the outriggers on both sides, and the 10.9-level high-strength bolts are used for layered preload fixation, and the preload force is applied three times to the design torque value to ensure uniform butt gaps and balanced force, and prevent deformation of the main beam and loosening of the connection.After the docking of the main beam is completed, the span, level, and verticality of the equipment are calibrated as a whole, and the deviation is fine-tuned to ensure that the installation accuracy of the main structure meets the national standard construction standards.

    Hoist and trolley installation

    After the installation and calibration of the main frame is completed, the hoisting core components, the hoist and the walking trolley, will be installed.First, the trolley and hoist are accurately hoisted to the center of the main beam track, and the wheel track and clearance of the trolley are adjusted to ensure that the trolley walks flexibly without caton and deviation.Then install the hooks, wire ropes, and pulley blocks, and wear and wrap the wire ropes in strict accordance with the specifications of the equipment instructions to ensure that the wire ropes are moderately elastic, neatly arranged, no extrusion, and no wear.Install the limit device and the lifting limit protection device, debug the upper and lower limits of the hook lifting, and the walking limit of the trolley to ensure that the limit action is sensitive and accurate, and the risk of rushing to the top and derailing is eliminated.All mechanical connection parts are fastened in place, and special lubricating greases are added to ensure the smooth operation of the transmission mechanism and improve the operating stability and service life of the equipment.

    Electrical and control system connection

    After the installation of the mechanical structure is completed, the wiring, wiring and debugging of the electrical control system will be carried out.Lay the cables in accordance with the electrical schematic diagram, standardize the routing and fixing of the cables, and do a good job of cable protection to avoid wear, pulling, moisture and leakage.Install the control cabinet, operation handle, emergency stop switch, limit alarm, walking warning light and other electrical accessories in turn.After the wiring is completed, strictly check the on-off, insulation performance, and grounding protection of the line to prevent short circuits, leakage, and wiring errors.Then debug the control system, test the basic functions of equipment start-stop, lifting, walking, variable speed, etc., optimize the control sensitivity, ensure smooth operation and accurate response, and debug safety alarm, overload protection, emergency braking and other protective functions to ensure the safe and stable operation of the electrical system.

    How to Ensure Safe Crane Operation After Installation?

    The completion of the installation does not mean the end of the construction. It must pass all-round testing, load testing, and safety acceptance. After confirming that the equipment meets the standards, it can be put into production and use.Standardized acceptance and commissioning is the core link to avoid late-stage safety accidents and ensure the compliance operation of equipment, and it is also an essential process for passing safety supervision and filing.

    Load testing and commissioning

    Load testing is the core standard for verifying the load-bearing performance and structural stability of Henan Mine Crane manufactured gantry cranes. It strictly follows the step-by-step test specifications for no-load, half-load, full-load, and overload.First, a no-load trial operation is carried out to test whether the equipment is stable in walking, lifting, and braking throughout the process, with no noise, no caton, and no offset.Then the rated load test is carried out, the standard counterweight material is hoisted, the normal operating conditions are simulated, and the structural force, orbital operation, and mechanical transmission status of the equipment are tested.Finally, an overload test of 1.25 times the rated load was carried out to verify the ultimate carrying capacity and structural stability of the equipment, and to investigate whether there are hidden dangers such as structural deformation, loose bolts, and cracked welds.All test data are recorded in detail, and the commissioning and delivery of the equipment can be completed after passing the test, and a complete commissioning and acceptance report can be issued.

    Travel and lifting tests

    Special operation and lifting tests focus on the accuracy and stability of equipment operations.The walking test detects the overall longitudinal walking of the gantry crane and the smoothness of the trolley’s horizontal walking throughout the whole process, investigates problems such as deviation, jitter, caton, and brake offset, and fine-tunes the track clearance and the accuracy of the walking wheel to ensure the smooth operation of the whole process at uniform speed.The lifting test focuses on detecting the smoothness of material lifting, the cushioning effect of start and stop, and the accuracy of height limit. It tests whether the low-speed and high-speed lifting and switching are smooth, whether the braking is accurate and reliable, and there is no slip hook or slip phenomenon.At the same time, the operating status of different spans and heights is tested to ensure the stable operation of the equipment under all working conditions and adapt to the needs of various hoisting operations in the factory.

    Safety system inspection

    Comprehensive investigation of the safety system is the last line of defense to eliminate operational risks, covering all safety protection devices and emergency systems.Detect overload protection, overload limit, lifting height limit, walking stroke limit, emergency braking device, buffer, and anti-collision device one by one to ensure that all protective devices are sensitive, reliable, and triggered accurately.At the same time, check electrical grounding, leakage protection, warning devices, sound and light alarms, and emergency power-off systems to investigate electrical safety hazards.After completing the hardware testing, carry out safety operation and emergency response training for operators, clarify equipment operation specifications, contraindicated working conditions, and emergency plans for failures, and ensure the safe operation of equipment from the three parties of equipment, personnel, and system.

    What Affects the Cost of Installing a Gantry Crane?

    Many companies are concerned about the overall cost of installing heavy gantry cranes in existing factories. The installation cost of equipment is not a fixed value and is affected by multiple factors such as the current situation of the plant, the difficulty of transformation, equipment parameters, and construction standards.The overall cost is mainly divided into three major sectors. Accurate understanding of cost influencing factors can effectively control the budget and avoid overspending.

    Structural modification costs

    The cost of plant structure renovation is the sector with the largest budget fluctuations, which mainly depends on the original conditions of the plant.The carrying capacity of old factories and ordinary light steel structure factories is insufficient, and large-area steel structure reinforcement, ground hardening, foundation reinforcement, and space transformation are required. There are many processes, large consumables, and high transformation costs.The brand-new heavy-duty steel structure plant and the plant reserved for hoisting loads only need to be simply reviewed and fine-tuned, and the cost of transformation is extremely low.At the same time, the transformation of tonnage and span will also affect costs. Large-tonnage and large-span heavy-duty gantry cranes have higher requirements for reinforcement standards, and steel, concrete, and labor costs have increased simultaneously.The cost gap between local transformation and overall reinforcement is significant, and accurate pre-evaluation can effectively avoid excessive transformation and waste of budget.

    Crane installation costs

    The installation cost of the equipment body includes labor, large-scale hoisting equipment, construction consumables, and on-site commissioning costs.Henan Mine Crane manufactured large-tonnage heavy-duty gantry cranes have complex structures and bulky components. They require the cooperation of large cranes and the collaborative construction of multiple professional technicians. The construction cycle is longer and the installation labor and equipment rental costs are higher.The installation process of small-tonnage equipment is simple, the construction efficiency is high, and the installation cost is lower.In addition, the construction environment will also affect the cost. In scenarios where the plant space is small, the entry is difficult, and there are many cross-operations, the construction difficulty will increase, the construction period will be extended, and the installation cost will increase accordingly.3. The construction of standardized factories is convenient, which can effectively reduce the cost of installation and construction.

    Electrical and commissioning costs

    Electrical system and commissioning costs include cable laying, electronic control equipment installation, system commissioning, inspection and acceptance, safety supervision filing and other costs.High-end intelligent control system, frequency conversion speed regulation, remote monitoring, intelligent limit and other configurations, the cost of electrical accessories is higher, and the debugging process is more complex.The cost of basic conventional electronic control systems is lower.At the same time, compliance acceptance, third-party testing, and data filing are also fixed expenses. The regular construction team will assist in completing the testing, acceptance, and filing process throughout the process to ensure that the equipment is put into production in compliance with regulations and avoid additional costs for later rectification.

    How to Minimize Downtime During Installation?

    The biggest pain point of the installation of gantry cranes in the factory is the shutdown of construction, which affects normal production, resulting in loss of production capacity and delays in construction.Through scientific construction planning and refined management, downtime can be compressed to the maximum extent, construction transformation and production peaks can be realized in parallel, and production losses can be greatly reduced.

    Pre-installation planning

    Perfect pre-planning is the core prerequisite for reducing downtime.Complete all plant inspections, plan design, drawing confirmation, material procurement, and equipment stocking work before construction, and complete the construction filing with the safety supervision department in advance to avoid downtime due to plan changes, material shortages, and incomplete procedures in the middle of construction.Accurately plan the construction process, process convergence, and staffing, refine daily construction tasks, and eliminate invalid construction periods.At the same time, investigate construction risks in advance, predict possible problems during renovation and installation, and formulate emergency plans to avoid failures and delays in construction.The more adequate the pre-preparation, the higher the efficiency of on-site construction and the shorter the overall downtime.

    Phased installation

    The phased and zoned construction mode is adopted to replace the one-time shutdown of the whole plant.Divide the plant into production areas and construction areas, isolate the construction area, and only close a small area of working space, and the rest of the area will be used for normal production operations.According to the step-by-step construction of transformation, paving, installation, and commissioning, each process is immediately accepted for acceptance, compressing the single-stage construction cycle.For multi-span factories and large-area workshops, they can be constructed step by step and put into production step by step to avoid overall shutdown.Phased construction can balance the construction schedule and production needs to the greatest extent, and minimize downtime losses.

    Production coordination

    Do a good job of coordination between the construction team and the production team, and arrange construction and production at the wrong peak.Use night shifts, weekends, and downtime to carry out noisy and interfering construction processes, and carry out refined and low-interference installation and commissioning work during the day.Adjust the production plan in advance, transfer the production tasks in the construction area to the normal operating area, and rationally allocate production capacity.Set up full-time coordination personnel on site to co-ordinate construction progress and production arrangements, resolve cross-operation contradictions in a timely manner, and avoid mutual interference between construction and production.Through efficient collaboration, both equipment upgrading and normal production are realized, and the loss of production capacity caused by transformation and installation is minimized.

    Henan Mine Crane Factory Custom

    For the installation of heavy-duty gantry cranes in existing steel structure factories, the core logic is first evaluation, then verification, fine transformation, standardized installation, and strict acceptance.Not all factories can directly install equipment. It is necessary to evaluate the structural bearing capacity, load parameters and space size, and then carry out reasonable design and transformation according to the on-site conditions, cooperate with standardized installation, load testing and safety acceptance, so that the heavy gantry crane can truly adapt to the production environment of the original factory.

    Henan Mine Crane Factory can provide customized gantry crane solutions according to plant size, lifting weight, span, lifting height and actual operating needs, and carry out targeted design and engineering support based on on-site conditions.Whether it is the renovation of existing factories or the upgrading of heavy equipment, it can be matched from program design, equipment manufacturing to installation and commissioning, so that enterprises can improve their hoisting capabilities without blindly expanding their plant investment.If you are considering installing a heavy-duty gantry crane in an existing steel structure plant, please contact Henan Mine Crane Factory for customized solutions and project quotations.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Improve Overhead Crane Positioning Accuracy in Production

    How to Improve Overhead Crane Positioning Accuracy in Production

    How to Improve Overhead Crane Positioning Accuracy in Production

    The positioning accuracy of bridge cranes directly affects the efficiency, safety and yield of industrial production.Problems such as positioning offset, load swing, and poor parking can easily cause misalignment of workpieces and chaotic stacking of materials, causing beat lag, equipment wear and even safety hazards.

    Most companies only guarantee the basic operation of cranes, ignoring the systematic optimization of positioning accuracy.The positioning error of the crane stems from the superposition of mechanical, driving, sensing, environmental, and human factors.This paper analyzes the positioning accuracy standards and the causes of errors in a concise manner, and provides a complete set of high-precision optimization solutions.

    What Is Overhead Crane Positioning Accuracy

    Positioning accuracy

    Positioning accuracy, also known as absolute positioning accuracy, refers to the degree of matching between the actual docking position of the hook, load, and trolley and the preset target position. It is measured by millimeter-level tolerances, which intuitively reflects the precise operation level of a single operation of the equipment. It is the core index of the basic positioning ability of the equipment.

    Repeat positioning accuracy

    Repeated positioning accuracy refers to the coincidence and consistency of the actual docking position of the hook, load and trolley in multiple cycles of operation. It is used to measure the position and stability of the continuous operation of the equipment. It is a key indicator to ensure the standardization and stability of operating conditions.

    Key points of the relationship between the two

    Positioning accuracy and repeated positioning accuracy are independent of each other and complement each other. They are the two core dimensions for measuring the positioning ability of equipment.Equipment often has a typical state of stability but not accuracy: the position of multiple stops is highly consistent and the stability is excellent, but there is a fixed deviation from the preset target as a whole.

    • Manual operation scenario: the core depends on the accuracy of repeated positioning.Manual can identify and compensate for fixed absolute deviations in real time, and rely on the stable repetitive operation ability of the equipment to complete precise operations.
    • Automated unmanned production line scenario: absolute positioning accuracy is the core requirement.Accurate absolute positioning is a prerequisite for the coordinated linkage of multiple equipment and the stable operation of unmanned automation, which directly determines the accuracy and operating reliability of the production line.

    Positioning accuracy evaluation dimension

    The positioning accuracy of bridge cranes is not a single parameter. It needs to be comprehensively evaluated by the five core dimensions to comprehensively measure the accuracy, stability and reliability of equipment operations. It is an important basis for the accuracy acceptance of industrial scenarios.:

    • Horizontal positioning error: Refers to the actual walking offset deviation of the main beam of the crane and the operating trolley in the XY working plane. It is the core technical index to determine the positioning accuracy of the whole machine, which directly determines the accuracy of the horizontal alignment of the material and the docking of the station.;
    • Residual load swing: After the crane completes the walking braking and shutdown, the continuous swing phenomenon of the crane due to inertia is the main hidden factor that causes the material drop point to shift, alignment failure, and rework rate to increase.;
    • Lifting height accuracy: Measure the deviation range between the actual lifting height of the hook and the preset standard height, which directly affects the accuracy of workpiece assembly and bonding and the regularity of multi-layer material stacking, which is the key assessment index of vertical operation accuracy;
    • Multi-cycle repeatability: It reflects the consistency and operating stability of the crane’s multiple start and stop positioning positions in long-term batch cycle operations, which is an important guarantee for standardized and automated continuous production.
    • Braking and parking distance: After the control system issues a parking instruction, the crane relies on the actual distance of the mechanical inertia to glide, and the stability of the braking response directly determines the final alignment accuracy and parking reliability.;

    Accuracy requirements of various industries

    The requirements for crane positioning accuracy under different production conditions vary significantly, and the corresponding accuracy standards are matched as needed, which can not only meet the needs of the production process, but also maximize the cost-effectiveness of equipment investment. The accuracy tolerance specifications for each scene are as follows:

    • Ordinary material handling scenarios: accuracy tolerance is ±100~300mm to meet the needs of basic material handling, transshipment, and stacking operations;
    • Precision assembly manufacturing scenario: accuracy tolerance ±10~50mm, suitable for parts docking, equipment assembly and other refined operations;
    • Heavy-duty scenarios of iron and steel heavy industry: accuracy tolerance ±20~100mm, suitable for heavy-duty handling conditions such as billet, steel coil, heavy forging, etc.;
    • Automated warehousing scenario: accuracy tolerance is ±5~20mm to ensure accurate warehousing, outbound and alignment stacking of materials;
    • Intelligent automated lifting system: accuracy tolerance is ±1~5mm, suitable for high-precision intelligent operations such as unmanned production lines and intelligent tooling docking.

    Common Causes of Overhead Crane Positioning Errors

    The inherent mechanical clearance and deformation are the root causes of long-term accuracy attenuation: the gear box backlash causes power idling and positioning dead zones; the lateral clearance of the wheel track causes lateral offset; the elastic deflection of the main beam under heavy load changes the position of the hook; long-term load and temperature difference cause cumulative deformation of the fuselage.

    Speed control defect

    Traditional fixed-speed cranes start and stop quickly and are easy to overtake; there is no close-range deceleration function, which is predicted by manual experience; the braking performance is unstable and the taxiing distance is not uniform; the low-speed control is poor, and frequent jog fine-tuning exacerbates wear and positioning deviation.

    Load swing effect

    The suspension load of the wire rope naturally forms a single pendulum structure.Start-stop mutation, commutation, heavy load, and high lift will all intensify the swing. After parking, the residual swing cannot be dropped immediately, and the drop point is offset and the production beat is stretched, which is the main obstacle to high-precision operations.

    Interference with environmental conditions

    Dirt, oil, wear and deformation on the surface of the track will change the coefficient of friction, causing fluctuations in braking distance and offset of walking position; wind in the semi-outdoor operating environment will form a lateral thrust on the fuselage and the crane, disrupting the trajectory; irregular loads with special-shaped workpieces and offset center of gravity are prone to irregular swing, which greatly weakens the positioning stability and alignment accuracy of the crane.

    Manual operation deviation

    There are differences in the parking prediction and jog operation habits of different operators. Frequent repeated fine-tuning not only exacerbates the loss of mechanical structure, but also causes the positioning effect to be unstable; at the same time, the operating methods of each shift are not uniform, which further leads to fluctuations in the accuracy of batch operations, making it difficult to form a standardized and consistent operating effect.。

    Improve Positioning Accuracy Through Better Motion Control

    Equipped with VFD frequency conversion speed regulation

    Variable frequency drive (VFD) is the core supporting device for high-precision crane operation. It can output a linear and smooth acceleration and deceleration curve, support wide-speed ratio multi-stage speed regulation and precise low-speed micro-motion operation, effectively avoid the mechanical impact and lifting swing problems caused by extremely fast start and stop, greatly reduce equipment loss, and maintain stable positioning accuracy for a long time.

    Optimize the acceleration and deceleration curve

    The acceleration and deceleration time can be dynamically matched according to the actual load weight and lifting height, effectively suppressing the lifting swing under heavy-duty conditions; at the same time, a low-speed creep interval is set at the front end of the target station to allow the crane to approach the stop smoothly and accurately, completely avoiding the problem of inertial over-range.

    Soft start-stop control strategy

    Completely avoid the start-stop power mutation, effectively suppress the residual swing of the crane, ensure that the positioning of each stop is highly consistent, buffer the mechanical impact of the transmission system, greatly delay the aging speed of the equipment and the attenuation of positioning accuracy, and achieve long-term stable and accurate operation results.

    Dual-axis independent speed control

    The dual-axis independent frequency conversion and speed regulation scheme of the main beam and the trolley is adopted, which can realize synchronous deceleration in both directions, linkage and oblique precision positioning, and is perfectly adapted to the layout of complex stations and multi-process cross-operation, significantly improving the alignment accuracy and overall operating efficiency.

    Use Positioning Sensors for More Accurate Crane Movement

    Laser positioning system

    The positioning system can achieve 1mm absolute positioning accuracy and 0.3mm ultra-high repeated positioning accuracy, can effectively avoid the positioning deviation caused by wheel slippage and wheel diameter wear, has wide temperature adaptability, can be stably adapted to all kinds of harsh industrial and mining environments, and does not require frequent zero-return calibration, and has strong operating stability. It is an excellent positioning solution for high-end automated cranes.

    Encoder position detection

    The absolute encoder can be powered off to remember the position data, no need to repeat the zero-return calibration, no cumulative positioning error throughout the process, and higher stability; the incremental encoder has a simple structure and outstanding cost performance. It is suitable for motor and wheel end installation under conventional working conditions, and can stably meet the needs of high-precision positioning operations in the equipment.

    RFID magnetic positioning system

    By embedding RFID identification tags in fixed workstations, the crane can automatically calibrate the coordinate data when it runs to the specified location, effectively eliminating the positioning drift caused by long-term operation of the equipment, stably achieving 10mm positioning accuracy, highly adaptable to repetitive cycle operation conditions, and can be seamlessly linked with the PLC control system to achieve automatic and accurate alignment.

    Machine vision positioning

    The system relies on industrial cameras to collect characteristic images of stations and workpieces in real time, accurately calculate the alignment offset and automatically complete dynamic correction, and realize fully autonomous intelligent alignment. It is the core key technology for intelligent factories to realize unmanned lifting, precision assembly, and automated palletizing operations.

    Add Anti-Sway Control to Improve Load Placement

    The swing of the crane is the core problem that causes the crane’s blanking offset and misalignment of positioning, which directly restricts the landing of high-precision automated operations.At present, the mainstream anti-swing technology in the industry can be divided into two categories: passive anti-swing and active closed-loop anti-swing, which are adapted to different working conditions and scenarios to accurately solve the problem of swing deviation.:

    • Passive anti-swing technology: relying on the mechanical buffer structure to suppress the swing of the crane, the structure is simple, the operation and maintenance cost is low, and it is suitable for ordinary indoor operation scenarios with stable working conditions and no external interference. It can only meet the basic anti-swing needs and cannot cope with wind and heavy-duty offset interference under complex working conditions.
    • Active closed-loop anti-swing technology: through real-time monitoring of pendulum angle and closed-loop control of dynamic speed regulation, it adaptively cancels various types of operation interference, realizes near-zero swing of the crane, stops and stabilizes, greatly improves the efficiency of lifting operations, the accuracy and safety of landing points, and adapts to high-precision and unmanned operation scenarios.

    Integrate PLC and Automation Systems

    PLC core control logic

    As the core of the automation control of the whole machine, the PLC system can collect the position data of high-precision sensors in real time, dynamically compare the deviation value of the target station and the actual position, and simultaneously output speed control correction instructions to the frequency conversion drive system to achieve real-time correction throughout the process and continuously stabilize the positioning accuracy of the equipment.

    Preset station automatic positioning

    The system supports pre-entry and curing of commonly used station coordinate parameters. During the operation process, the equipment can independently plan the operating path and accurately complete the alignment and docking, completely avoiding the random deviation caused by manual operation, and effectively ensuring the consistency and stability of positioning accuracy under mass production conditions.

    Closed loop feedback control system

    The system builds a high-frequency closed-loop control system of “sensing and detection-PLC operation-drive speed regulation-position correction”, which can dynamically converge positioning deviations in real time, has strong anti-interference ability and operating stability, and the overall control effect is significantly better than traditional open-loop control, fully meeting the requirements of millimeter-level high-precision operations.

    Factory automation system docking

    The crane control system can be connected to MES, SCADA, and warehouse management systems, automatically receive operation tasks, realize unmanned transfer and station linkage, adapt to Industry 4.0 intelligent production, and upload data synchronously for equipment monitoring and optimization.

    Mechanical Maintenance Is Essential for Positioning Accuracy

    A precise electronic control system can only optimize the operation control deviation, and cannot offset the inherent positioning errors caused by mechanical structure wear and assembly deformation. Standardized and normalized mechanical operation and maintenance is the core bottom line to ensure the long-term positioning accuracy of the crane.Targeted and refined operation and maintenance content can be divided into four modules to avoid mechanical accuracy loss in all directions:

    • Operation and maintenance of walking mechanism: regularly calibrate the wheel parallelism, track flatness, and spacing parameters, deal with track wear, fouling, and deformation problems in a timely manner, eliminate wheel deviation and rail gnawing, and avoid horizontal walking positioning offset from the source.
    • Operation and maintenance of transmission mechanism: Normalize the detection of gearbox backlash, coupling coaxiality and fastening status, and carry out lubrication and maintenance work as needed to reduce transmission air range and power transmission deviation, ensure stable power output, and avoid positioning dead zone problems.
    • Operation and maintenance of the braking system: regularly verify the sensitivity and braking torque of the braking system, unify the braking and taxiing distance of the equipment, solve problems such as unstable braking, over-range parking, and inconsistent points, and ensure the stability of each parking positioning.
    • Operation and maintenance of lifting mechanism: regularly check the wear, tightness, reel working conditions, pulley smoothness and hook status of the wire rope, and replace aging and worn accessories in time to eliminate the positioning deviation of vertical lifting operations.

    Calibrate the Crane Positioning System

    The long-term continuous operation of the crane will cause problems such as system parameter drift and mechanical structure loss, and the positioning deviation will continue to accumulate, reducing the operating accuracy.In order to ensure the stability of equipment positioning for a long time, a standardized and normalized system calibration mechanism needs to be established. The core control measures are divided into the following five categories:

    • Set up a reference zero point: fix the reference zero point of equipment operation, unify the calibration reference standard of all positioning parameters, and avoid the systematic positioning error caused by the reference offset from the root cause.
    • Regular sensor calibration: Perform accuracy verification and parameter correction of various sensor equipment such as laser positioning, encoders, RFID, etc. in accordance with standard cycles to ensure accurate and reliable sensor detection data.
    • Postoperative zero-return calibration: After the equipment overhaul, replacement of core accessories, and structural debugging are completed, the zero-return calibration must be re-calibrated to eliminate the assembly and positioning deviations caused by disassembly and assembly changes.
    • Deviation data control: Normalize the deviation of the alignment accuracy of the measured equipment, completely record the operating data, form an accuracy ledger, and provide data support for parameter optimization and equipment rectification.
    • Customized calibration cycle: Formulate differentiated calibration cycles based on equipment load conditions, operating frequency, and operating environment, predict equipment aging and accuracy attenuation problems in advance, and realize preventive maintenance.

    How to Choose an Overhead Crane for High-Precision Production

    Clarify the requirements of accuracy and working conditions

    The selection of equipment needs to be combined with the tolerance requirements of the production process, the frequency of daily operations, and the comprehensive matching configuration scheme of manual and automatic operating modes to accurately fit the actual working conditions, avoid the problem of excess or insufficient accuracy, and ensure the accuracy and practicality of the operation while taking into account the economy of equipment investment.

    On-demand matching control system

    Optional VFD+ mechanical limit for conventional working conditions; optional VFD+ incremental encoder for general manufacturing; optional VFD+ laser/absolute encoder + PLC for precision warehousing; optional LASER + anti-swing + closed-loop PLC for high-end automation; super-precision intelligent production line superimposed machine vision and MES integration.

    Selection based on working conditions and environment

    Equipment selection needs to comprehensively consider equipment parameters such as rated load, operating span, lifting height, and working level, combined with complex working conditions such as on-site temperature, humidity, and dust, and scientifically match the adapted equipment protection level and high stability control system to ensure the stable operation of the equipment around the clock and long-term reliable operation.

    Reserve space for automation upgrade

    When selecting equipment, expansion interfaces such as remote control, data interaction, and intelligent monitoring should be reserved in advance. They are compatible with cutting-edge intelligent technologies such as digital twins and predictive maintenance, which can meet the needs of subsequent intelligent iterative upgrades of equipment, and reserve sufficient expansion space for the overall transformation and digital upgrading of smart factories.

    Conclusion

    The positioning accuracy of bridge cranes is affected by many factors such as mechanical structure, drive, sensing, control, and operation and maintenance.Load swing, abnormal parameters, component wear, sensing and operating deviations will all cause alignment offset, affecting operating efficiency and equipment life.

    In view of the above problems, Henan Mine Crane can improve the positioning accuracy and stability of cranes through mechanical repair, parameter optimization, sensor upgrade, anti-swing, PLC closed-loop control, and regular calibration of the whole process optimization plan, reduce alignment errors and mechanical losses, adapt to precision manufacturing, intelligent warehousing and other scenarios, and help efficient and intelligent operation of lifting operations.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Improve Energy Efficiency of Port Cranes

    How to Improve Energy Efficiency of Port Cranes

    How to Improve Energy Efficiency of Port Cranes

    Port cranes are among the largest energy consumers at any container terminal, accounting for as much as 40% of total port electricity use. As electricity tariffs rise and environmental regulations tighten, port crane energy efficiency has shifted from a sustainability talking point to a core operational priority. This guide covers the technologies and practices, from regenerative braking to smart automation — that terminal operators use to cut crane energy consumption without sacrificing throughput.

    Why Energy Efficiency Matters for Port Cranes

    High Energy Consumption in Modern Container Terminals

    Henan Mine Crane manufactured port cranes operate on a demanding duty cycle: continuous lifting, heavy-duty motors running at variable loads, long shifts (often 16–24 hours a day), and sharp power spikes every time a container is hoisted. Ship-to-shore (STS) cranes are particularly power-intensive because they combine high lifting loads with frequent acceleration and deceleration, creating short bursts of peak demand that strain terminal electrical infrastructure. Because port cranes are the biggest energy consumers within a port, they also represent the single best opportunity for facility-wide energy savings.

    Benefits Beyond Lower Electricity Bills

    ImprovingHenan Mine Crane manufactured crane energy efficiency delivers value well beyond the utility bill:

    • Lower operating costs by decreasing fuel and electricity consumption
    • Less carbon emissions end to end, and in port (positive environmental reputations and benefits, along the terminals and ships). Offsetting added carbon emissions in ports (who gets credit?).
    • Increased lifetime of the equipment due to reduction of strain on the equipment introduced by more energy efficient drive systems
    • Enhanced reliability, fewer surprise failures resulting from bursts of overloaded motors and worn parts
    • Increased competitive position (as beneficial cargo owners and carriers favor terminals with proven sustainability credentials)

    Understand Where Port Cranes Consume the Most Energy

    Before you invest in upgrades, it’s useful to find out where your energy is going.

    Hoisting is the most power hungry per cycle – sheer lifting of a loaded container against gravity stresses the motor to its maximum. Trolley travel – lifting the load horizontally is the second most power hungry, since there is another layer of power consumption – constant acceleration (and deceleration). Gantry travel to move the entire crane along the rails is not very power hungry as the walk long distances to pick up a (second or third) container.

    A more subtle but just as significant component of waste is idle time and standby power consumption. The auxiliary systems cabin lights, air conditioning, hydraulic pump, and control electronics drain power even when the crane is not moving containers. Diesel-operated cranes also consume fuel while their engines are left running while they wait.

    Install Regenerative Braking Systems

    How Regenerative Braking Works

    When a loaded container is lowered or a trolley decelerates, the crane’s motor acts briefly as a generator, converting kinetic and potential energy back into electricity instead of dissipating it as heat through a braking resistor. Regenerative variable frequency drives (VFDs) capture this energy and feed it back into the crane’s power system or the terminal grid.

    Recovering Energy During Lowering Operations

    Because Henan Mine Crane manufactured port cranes regenerate more than half of the energy used to lift a container when lowering it back down, this single technology addresses one of the largest efficiency gaps in crane operation. For high-duty cranes with frequent loaded-lowering cycles, STS cranes in particular, regenerative drives typically achieve a 20–40% net reduction in overall electricity consumption, depending on workload and cycle frequency, while also eliminating the maintenance burden of resistor-based braking.

    Suitable Crane Types

    Regenerative braking is applicable across the major Henan Mine Crane Factory supply port crane categories:

    • STS cranes:highest savings potential due to heavy, frequent lifts
    • RTG cranes:significant fuel savings when paired with hybrid diesel-electric systems
    • RMG cranes:consistent savings from repetitive stacking cycles

    Upgrade to High-Efficiency Electric Drive Systems

    Variable Frequency Drives (VFDs)

    VFDs control of speed and torque is achieved through varying the frequency and voltage of the power supplied to the crane‘s motors, rather than running them at a constant speed regardless of load. This fine-tuning results in less wastage and more efficient operation, as well as a smoother soft-start/soft-stop cycle. Payback time is often 6–12 months due to material savings on energy bills and maintenance and increased efficiencies.

    High-Efficiency IE3 and IE4 Motors

    Another way to improve energy efficiency is to use IE3 (Premium Efficiency) or IE4 (Super Premium Efficiency). This upgrades to motors offering the lowest electrical losses through the duty cycle of the crane (at part loads in particular).

    Permanent Magnet Motors

    They can be more efficient and offer higher power densities than induction machines. As a result they are more attractive for new-build cranes where the cost can be justified by lifecycle energy savings.

    Intelligent Motor Control

    In addition, many modern drives incorporate cumulative anti-sway algorithms, load torque memory, and slack-rope detection, all of which previously depended on additional hardware. Using these integrated capabilities in the drive control logic decreases the overall energy requirement and drives more simple.

    Optimize Crane Operating Speed

    Energy usage doesn’t increase proportionally with speed; operating a crane at its nominal maximum rated speed for each motion has the potential to compensate excess energy usage in cycle time.

    • Avoid excessive high-speed for short-distance or light load transportation.
    • Employ load dependent, adaptive speed control , If the applied speed is controlled by load then the write speed should be controlled according to the real load weight, the weight of maximum load is nothing.
    • Use a smooth acceleration and deceleration curve instead of a sudden start/ stop
    • Less mechanical stress to brakes, gearboxes and cables thereby multiplying energy savings with reduced maintenance costs during lifetime.

    Use Smart Crane Automation and Energy Management Systems

    Digital tools supplement hardware upgrades and provide more intelligence to Henan Mine Crane Factory supply port crane energy efficiency.

    Real time energy monitoring allows Terminal operators to have inground transparency on energy consumption by crane, move and shift a key component for waste identification. Automated route optimization reduces trolley and gantry travel by intelligently determining the shortest path from pick-up to delivery. Load scheduling based on Artificial Intelligence allows to coordinate cranes’ operational windows to prevent multiple cranes peaks on power usage happening at the same time.

    Even at scale peak power management is particularly beneficial: research on ship-to-shore quay crane scheduling has demonstrated that, in combination with the adoption of joint operational guidelines, common energy peaks can be reduced by as much as 50%, at the cost of less than 0.5 minutes per hour increase in vessel service time a very significant cost-saving for a very minimal productivity tradeoff. Lastly, remote diagnostics and predictive maintenance identify inefficiencies: worn bearings, misaligned wheels, worn down motors.

    Electrify Diesel-Powered Port Cranes

    Converting RTG Cranes from Diesel to Electric

    Diesel RTG cranes are still used at terminals with limited electrical infrastructure, but they have a much higher fuel and maintenance cost than the electrified crane. There are several electrification conversion routes, depending on the infrastructure in place and budget.

    Cabling reel system – cable reel and feeding cable transfer power from the grid to the crane, otherwise the portable diesel generator just moves the crane to the next pile. Busbar power supply the RTG is fully electric running on a low electrified rail and avoids diesel entirely- crane is available more often due to no refueling.

    Hybrid RTG solutions provide a compromise: a smaller diesel generator can charge a battery system to which the crane can switch in battery mode and draw on only in peak power situations, charging back to the battery in braking mode like a hybrid car. This design can even be fitted as an upgrade to already dsl-electric equipped cranes, appealing to terminals not yet ready for a complete shift to electrification.

    Battery-assisted crane technology, including supercapacitor and lithium-ion systems, further smooths power demand and enables engine shutdown during idle periods.

    For terminals evaluating the switch, electric RTG energy costs typically run 40–60% of equivalent diesel RTG fuel expenditure, with infrastructure investment generally paid back within five to eight years, a timeline that shortens further wherever electricity tariffs are low relative to diesel prices or government decarbonization incentives are available.

    Reduce Energy Loss Through Proper Maintenance

    Even the most efficient crane technology underperforms if poorly maintained. A structured maintenance program should include:

    • Lubrication of mechanical componentsto reduce friction losses in gearboxes and wire ropes
    • Wheel and rail alignmentchecks, since misalignment increases rolling resistance and energy draw
    • Brake inspectionto ensure regenerative and mechanical braking systems function as designed
    • Motor and gearbox maintenanceto catch efficiency-robbing wear before it worsens
    • Electrical system inspection, including cabling, contactors, and VFD components, to prevent power quality issues and unplanned energy losses

    The financial impact of neglecting maintenance is often underestimated. A misaligned wheel or a slightly worn brake pad may seem minor, but across thousands of duty cycles per month, the added rolling resistance and friction translate into measurable extra kilowatt-hours per move. Many terminals are shifting from calendar-based maintenance schedules to condition-based and predictive maintenance, using vibration sensors, thermal imaging, and motor current signature analysis to detect wear before it affects energy consumption. This approach not only preserves efficiency gains from other upgrades, a poorly maintained crane with a state-of-the-art VFD will still underperform, but also reduces the frequency of costly emergency repairs that take equipment out of service entirely. For terminals managing large fleets, integrating maintenance data with the same energy monitoring platform used for KPI tracking makes it easier to see, in real time, when a specific crane’s energy-per-move figure starts drifting upward, often the earliest warning sign of a developing mechanical issue.

    Optimize Terminal Operations to Reduce Crane Energy Consumption

    Equipment upgrades address only part of the equation, operational planning is equally important.

    Intelligent container scheduling particularly to optimize yard-truck scheduling reduces unnecessary repositioning, especially those moves that push or pull a container from where a crane already is. Procuring empty moves (i.e.: moves where the truck travels without the container) again decreases energy rates by averting trips without a load. Limiting the waiting time between moves maintains a lower duration for the use of auxiliary systems. Including the yard-truck, RTGs, and quay cranes in the scheduling decisions prevents concurrent -power-intensive- processes that increase demand. Aggregating those scheduling decisions in the scope of a TOS guarantees that the energy considerations will not be limited to one afterthought during the planning process.

    One operational technique gaining traction is quay crane double cycling, where a crane discharges an import container and loads an export container in the same cycle instead of running separate discharge and load cycles. Beyond the productivity benefit, double cycling changes the crane’s power demand profile, and research into peak-shaving policies for double-cycling operations has shown that carefully timed delays between crane movements can flatten power peaks without materially affecting throughput. Similarly, staggering the start times of multiple quay cranes working the same vessel, rather than allowing them to hoist simultaneously, avoids compounding peak demand charges, which in many markets represent a significant and controllable share of a terminal’s total electricity bill. None of these changes require new hardware; they require rewriting operating procedures and, in more advanced terminals, encoding these rules directly into the TOS so that energy-aware scheduling happens automatically rather than depending on manual planner judgment.

    Upgrade Lighting and Auxiliary Systems

    Auxiliary loads are a smaller share of total consumption but are among the easiest wins to implement:

    • LED lightingon cranes and in yards, replacing high-energy metal halide or sodium fixtures
    • Smart lighting controlthat dims or shuts off lighting in unused areas
    • Efficient cooling systemsfor electrical cabinets and control rooms
    • Energy-efficient cabin air conditioning, which can be a meaningful auxiliary load on cranes operating in hot climates

    While auxiliary systems typically account for a small fraction of a crane’s total energy footprint compared to hoisting and travel motors, they run continuously, often 24 hours a day regardless of whether the crane is actively handling cargo, which makes their cumulative cost add up over a year. Replacing floodlights across an entire container yard with LED fixtures, for example, commonly cuts yard lighting energy use substantially while also improving visibility for operators and reducing maintenance callouts, since LEDs last far longer than the metal halide or high-pressure sodium fixtures they replace. Motion- or schedule-based smart lighting controls compound these savings further by ensuring yard areas without active operations aren’t lit at full brightness overnight. These are typically the lowest-cost, fastest-payback items on any energy efficiency roadmap, making them a sensible starting point for terminals just beginning to formalize an energy program.

    Renewable Energy Integration for Port Cranes

    Ports are increasingly pairing crane electrification with on-site renewable generation and storage:

    • Solar powerfor auxiliary systems such as lighting and control electronics
    • Battery energy storage systems (BESS)to buffer peak crane demand and store regenerated braking energy
    • Microgrid integration, allowing ports to manage crane, yard, and building loads as a coordinated system rather than isolated draws on the grid
    • Shore power infrastructure, which lets docked vessels draw electricity from the terminal grid instead of running onboard generators, reducing emissions and noise portwide

    The economic case for renewables at ports has strengthened considerably as crane electrification increases overall electricity demand. Ports that combine on-site solar generation with battery storage can offset a portion of daytime crane and yard consumption directly, reducing exposure to peak-hour utility tariffs. Battery storage plays a dual role in this context: beyond capturing solar generation, it can also absorb regenerated braking energy from cranes that would otherwise be lost if the crane’s own storage system is already at capacity, then discharge it during subsequent peak-demand periods. This is where seaport microgrid concepts come in, rather than treating solar panels, battery storage, shore power, and crane loads as separate systems, a microgrid controller manages them as one coordinated network, automatically routing energy where it’s needed most and reducing the size (and cost) of grid connection upgrades that would otherwise be required to support a fully electrified crane fleet. For ports operating under strict emissions regulations, such as EU ports under the Green Deal framework or terminals subject to California Air Resources Board rules, this kind of integrated renewable and storage strategy is increasingly becoming a compliance necessity rather than an optional upgrade.

    Measure and Benchmark Energy Performance

    You can’t improve what you don’t measure. Terminal operators should track a consistent set of KPIs across their crane fleet:

    • kWh per container handled:the core efficiency metric for comparing cranes and shifts
    • Energy per operating hour
    • Regenerated energy percentage:how much braking energy is being recovered and reused
    • Peak demand: critical for managing utility demand charges
    • Crane utilization: since idle cranes still draw auxiliary power

    Continuous performance improvement means reviewing these KPIs on a regular cadence, not just during equipment audits, and using the data to prioritize which upgrades deliver the fastest payback.

    Benchmarking is most useful when it’s comparative, not just absolute. Tracking kWh per container handled for a single crane in isolation tells you whether that crane is trending up or down over time, but comparing the figure across every crane in the fleet, same model, same duty cycle, quickly surfaces outliers that warrant a maintenance check or an operator coaching conversation. Many terminals now run a formal energy audit annually or biannually, pairing automated monitoring data with a physical inspection of a sample of cranes to validate that sensor readings match real-world conditions. The output of that audit should feed directly back into the prioritization framework above: a crane consistently underperforming its peers on kWh per move is a stronger candidate for VFD retrofit or drive replacement than one already performing near the fleet average, even if both are the same age.

    Common Mistakes That Increase Port Crane Energy Consumption

    Several recurring issues undermine energy efficiency efforts:

    • Oversized motorsthat run inefficiently at partial load
    • Excessive idle time, particularly on diesel-powered equipment left running between moves
    • Poor maintenance, allowing friction and misalignment losses to accumulate
    • Outdated control systemslacking VFDs or regenerative capability
    • Lack of operator training, since operating habits (acceleration patterns, speed selection) materially affect energy use

    Each of these mistakes tends to compound the others. An oversized motor run by an untrained operator using maximum speed for every move, on a crane that hasn’t had its brakes inspected in months, isn’t just missing one efficiency opportunity — it’s stacking multiple sources of waste on top of each other. This is why energy efficiency audits should look at equipment specification, maintenance records, control system capability, and operator practices together, rather than treating them as separate line items. In practice, operator training is one of the most cost-effective fixes on this list: it requires no capital investment, can be implemented immediately, and studies of crane and hoist operations consistently show that operating habits, smooth versus abrupt acceleration, appropriate speed selection for load weight, minimizing unnecessary idling, can shift energy consumption by a meaningful margin even on identical equipment.

    Choosing an Energy-Efficient Port Crane for New Projects

    Features to Look For

    When specifying new cranes, terminal operators should prioritize:

    • Regenerative drive systems
    • Intelligent automation and route optimization
    • Built-in real-time energy monitoring
    • Hybrid or fully electric power options
    • High-efficiency (IE3/IE4) or permanent magnet motors
    • Predictive maintenance capabilities

    Questions to Ask Your Crane Manufacturer

    Buyers should ask manufacturers for documented energy consumption data per move under realistic duty cycles, confirmation of regenerative braking efficiency, available retrofit paths for future upgrades, and total cost of ownership projections that account for electricity or fuel costs over the crane’s expected lifespan — not just the purchase price.

    It’s worth pressing manufacturers for figures that reflect your terminal’s actual conditions rather than idealized test-bench numbers. A crane’s rated energy consumption under a manufacturer’s standard duty cycle can differ meaningfully from its real-world performance in a terminal with different container weight distributions, ambient temperatures, or move frequencies. Ask for reference sites with a similar throughput profile to yours, and where possible, request access to that site’s actual monitored energy data rather than relying solely on vendor projections. Finally, clarify what happens after the warranty period: some manufacturers offer performance guarantees tied to specific energy consumption targets, with penalties or corrective service included if the crane underperforms once in service — a detail that can materially change the total cost of ownership calculation in your favor.

    Frequently Asked Questions

    How much energy can modern port cranes save?

    The use of regenerative braking, VFDs and automation can achieve a saving of 20–40% in energy consumption of a crane and full electrification of diesel RTGs can give a reduction in energy consumption to 40–60% of the previous diesel fuel costs.

    Which type of port crane is the most energy efficient?

    For fully electric RTG and RMG cranes are generally the most efficient types of those examined. Without any diesel for fuel they perform extremely well especially in regenerative braking able to replace 100% of energy used in a typical cycle. Hybrid RTGs provide a compromise were full electrification isn‘t possible.

    Does automation reduce crane energy consumption?

    Yes. Automated route optimization, speed regulation and coordinated scheduling can eliminate much movement, power demand peaks, with operational scheduling reducing peak demand by as much as 50%.

    Is retrofitting older port cranes worthwhile?

    Generally, yes. Many retrofits can be added to current cranes hybrid power packs, VFD upgrades, and regenerative brakes to name a few often recouping within a few years through saved fuel and electricity (without the capital cost of full replacement).

    How often should energy performance be monitored?

    Energy performance should be monitored continuously by means of real time monitoring system, s combined by periodic review of KPIs and formal energy audits which help identify any problem that are not detected by monitoring on daily basis.

    What is the fastest way to start improving port crane energy efficiency?

    Simple low-cost, low-disruption process improvements such as LED lighting, operator training and minimal maintenance adjustments (wheel alignment, brakes) normally can pay-off quickly, and are often both implemented and completed before more capital-intensive processes are scheduled for planning (electrification, VFD retrofits).

    Do energy-efficient port cranes cost more upfront?

    Cranes with regenerative drives, high-efficiency motors, or full electrification typically have higher initial costs than traditional diesel or non-regenerative equipment, but if savings on fuel and electric costs over five to eight years payback is achieved, the investment in efficiency will have paid for itself by the end of the crane‘s operating life.

    Henan Mine Crane Factory Custom

    Improving the energy efficiency of port cranes requires more than adopting a single technology. The best results come from combining energy-efficient mechanical design, regenerative drive systems, intelligent automation, predictive maintenance, and operational optimization into one integrated solution. Whether you’re upgrading an existing terminal or investing in a new container handling system, choosing the right crane configuration can significantly reduce energy consumption, lower lifetime operating costs, and improve overall terminal performance.

    At Henan Mine Crane Factory, we design and manufacture reliable port crane solutions that help terminals achieve higher productivity with lower energy usage. From STS cranes, RTG cranes, and RMG cranes to customized lifting solutions, our engineering team works closely with customers to recommend equipment tailored to their handling capacity, operating environment, and long-term efficiency goals. If you’re planning a new project or looking to modernize your existing crane fleet, we’re ready to help you find a dependable, cost-effective solution that delivers lasting value.

    Henan Mine CraneDiscuss your requirements ↗