Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

分类: Technical Resources

Crane selection, technology, operation and purchasing knowledge.

  • Crane Factory Direct vs. Distributor: Which Should You Choose?

    Crane Factory Direct vs. Distributor: Which Should You Choose?

    Crane Factory Direct vs. Distributor: Which Should You Choose?

    Buying a crane is rarely a small decision. A single overhead crane can run from the low five figures into six figures, and the wrong sourcing choice doesn’t just cost money up front it can cost you in lead time, downtime, and years of frustrating parts orders. The crane factory direct vs. distributor decision sits at the center of that risk, and most buyers make it without fully understanding what they’re trading away.

    This guide breaks down exactly what separates a factory-direct purchase from a distributor purchase, where the real cost differences come from, and how to decide which model fits your facility, budget, and timeline.

    Quick Answer: Factory Direct vs. Distributor at a Glance

    Factor Factory Direct Distributor
    Upfront cost Generally lower (no middleman markup) Higher (includes distributor margin)
    Lead time Longer (built to order) Often shorter (stocked or regional inventory)
    Customization High direct engineering input Limited to what the OEM allows the dealer to configure
    Brand/model choice Locked to one manufacturer’s line Often multi-brand
    Local service & parts Depends on manufacturer’s own network Usually stronger, especially for established dealers
    Communication Direct with engineers, but can be slower across time zones Faster local point of contact
    Best for Large, complex, or specialized orders Smaller, faster, or first-time purchases

    If you need a highly customized, high-volume, or specialized crane and have flexibility on timeline, factory direct usually wins on cost and control. If you need something installed soon, want a single point of local contact, or aren’t sure exactly which brand fits your application, a distributor is usually the safer path.

    What Factory Direct Actually Means in the Crane Industry

    Factory-direct purchasing means buying straight from the company that designs, engineers, and manufactures the crane with no dealer, trading company, or sales intermediary in between. You’re working directly with the OEM’s sales engineers from quote to delivery.

    This model is most common with manufacturers who are vertically integrated, meaning they control most of the production chain steel fabrication, electrical systems, hoists, and final assembly in-house rather than buying in finished subassemblies from third parties. Vertical integration matters because it gives the manufacturer (and indirectly the buyer) more control over the supply chain that would otherwise be diluted at each outside vendor stage.

    Factory-direct doesn’t automatically mean “small operation” or “no support.” Many large OEMs run factory-direct sales teams precisely because they want to control specification accuracy, pricing, and the engineering relationship with the end user particularly on custom or heavy-duty cranes where a generic dealer questionnaire isn’t enough to capture the application’s real requirements.

    What it does mean is that you are the manufacturer’s only point of contact. There’s no dealer absorbing communication gaps, smoothing over scheduling conflicts, or stepping in if the OEM is slow to respond.

    Whether you’re comparing factory-direct suppliers or local distributors, selecting the right partner is just as important as selecting the right crane.

    Henan Mine Crane offers customized crane solutions, engineering consultation, factory inspections, international shipping support, and technical assistance for customers worldwide. Contact our team to discuss your lifting requirements and receive a tailored solution with competitive pricing and reliable long-term support.

    What a Crane Distributor Does and Doesn’t Do

    Crane dealer is an intermediate service provider connecting equipment manufacturers and end-users, responsible for purchasing and reselling complete cranes and accessories, relying on regional inventory, local sales and after-sales team to provide customers with one-stop services such as installation, maintenance and so on.

    Dealers can provide customers with three core service advantages:

    Multi-brand Product Selection Channels

    Customers can rely on a single dealer docking multi-brand crane product line, without having to dock one by one to the original equipment manufacturers. Can be completed within a unified docking channel of different brands of equipment, technical parameters, configuration and price comparison, effectively simplify the pre-selection process, reduce communication costs, significantly improve the efficiency of procurement selection.

    Localized Service Capability

    Dealers in the industry generally adopt a grid-based regional layout, equipped with licensed, systematic training of technicians around the manufacturer to ensure that customers can quickly arrive at the scene around the plant.

    Relying on the advantages of nearby service, we can efficiently complete the equipment site survey, supervision of the installation process, acceptance and commissioning and emergency repair of unexpected failures and other on-site work, so as to achieve a rapid response to the needs of closed-loop problem solving and minimize the loss of equipment downtime.

    Integrated Package Service Program

    Dealers can provide customers with integrated packaged services, packages covering the whole chain of services such as equipment installation, commissioning, operator skills training, long-term maintenance contracts.

    All services are delivered in a unified and integrated manner, one-stop landing, without the need for customers to docking, separate negotiations, greatly simplifying the procurement and operation and maintenance of the cooperation process, so that the full cycle of the use of equipment to ensure a more complete and efficient.

    Dealers do not have the original R & D authority, can not independently complete the non-standard customization, need to be forwarded to the original factory to deal with, more communication links, customization cycle is longer. Most of the crane manufacturers to the distribution model instead of the terminal direct sales, with the dealer’s localization advantages, to provide customers with pre-sales assessment, after-sales operation and maintenance and parts protection services.

    Some mainstream crane manufacturers rely entirely on dealer sales, not directly facing the end customer, in order to protect the dealer’s service and parts revenue, solid local customer relations, to maintain the service quality of the entire distribution system and operational stability.

    Cost Comparison: Where the Price Difference Really Comes From

    The headline difference buyers care about most is price and on paper, factory direct is almost always cheaper. Direct manufacturer purchases tend to offer lower costs and direct communication with engineers, while dealer purchases typically carry higher prices due to the added markup of the middleman.

    That markup isn’t arbitrary. It funds:

    • Local inventory carrying costswarehousing, regional staff, and showroom or yard overhead
    • Pre-sale technical consultationtime spent by sales engineers helping you spec the right machine
    • Post-sale service infrastructuretechnicians, service trucks, and parts stock held closer to your facility

    For commoditized, standard-spec equipment, that markup can feel like pure overhead. For complex or first-time purchases, it’s effectively prepaid consulting and risk insurance.

    There’s a parallel pattern in other industrial sourcing categories that maps almost exactly onto cranes: buyers closer to the source of production get more control over specification, pricing, and packaging decisions, while distributor buyers are paying for the convenience of inventory that’s already landed, already cleared, and ready to ship.

    Factory-direct sourcing puts the buyer closer to raw material selection, production scheduling, and packaging decisions, while a distributor buys inventory from factories and resells it from local or regional stock a difference that changes the entire purchasing process. Neither model is universally cheaper;

    it depends on order complexity and volume. Factory-direct purchasing tends to become more attractive as order complexity and volume increase, while distributors remain the more practical choice for buyers who need a small quantity immediately or don’t want to manage production coordination themselves.

    Lead Times and Customization: Direct’s Biggest Advantage

    If your facility has an unusual bay width, a non-standard hook path, or specific duty-class requirements, factory direct gives you a real advantage: you’re talking to the people who will actually engineer the machine, not a sales rep relaying your requirements secondhand.

    That said, direct orders typically take longer to reach delivery. Direct manufacturer purchases come with the tradeoff of potentially longer lead times and communication barriers, compared to the faster access and broader guidance a dealer can offer. Custom-engineered cranes require structural calculations, sometimes coordination with your existing building records, and a full design review before fabrication even starts.

    A genuinely capable manufacturer direct or through a distributor should walk through a structured technical process before finalizing your spec, not just take a paint-color and hook-height order. Look for a partner who confirms span, lifting height, travel speed, hook path, and control interface against your actual facility data, and who can coordinate structural integration if you have an existing runway system already in place.

    If your facility already has crane infrastructure and you’re not changing duty class or capacity significantly, a distributor’s stocked or semi-stocked inventory may get you running again faster which matters enormously if you’re replacing a failed crane mid-production rather than planning a new installation.

    Service, Parts, and Warranty Support: Distributor’s Strongest Case

    This is where the distributor model earns its markup back. Dealer purchases typically come bundled with expertise, guidance through the buying process, and structured after-sales support. The core advantage of dealer purchases is access to a range of brands and models, hands-on expertise and guidance, and after-sales support while direct purchases can come with limited brand options and potential communication barriers down the line.

    Warranty servicing is a particularly underrated factor. If something goes wrong post-installation, you want a clear, fast escalation path. Buying through an established local dealer generally means a technician is a phone call away, while factory-direct warranty claims may have to route through a national or even international support desk, depending on where the manufacturer is based.

    There’s a real difference, too, between buying from a manufacturer or dealer versus a third-party trading company. Going through a trading company can introduce extra friction specifically around warranty coordination, since claims may need to route through the trading company rather than straight to the manufacturer. Warranty claims and servicing arranged through a trading company can become more complex, since they have to be coordinated through that company rather than handled directly with the manufacturer.

    This is also where the proprietary parts issue becomes relevant, regardless of which sourcing path you choose. Many cranes are built with OEM-exclusive components that can only be sourced through that manufacturer or an authorized distributor. Proprietary parts are components designed and manufactured by the original equipment manufacturer and exclusive to that brand, meaning they’re typically unavailable through third-party distributors and must be purchased directly from the OEM or an OEM-authorized distributor.

    If you go factory direct on a brand with heavy proprietary parts reliance, you may find yourself permanently dependent on that single relationship for every future repair.

    Hidden Risks Each Model Carries

    Factory direct risks:

    • Single-brand lock-in.You only see one manufacturer’s product line, so there’s no built-in comparison shopping unless you run a separate RFQ process yourself.
    • Proprietary parts dependency.As noted above, OEM-exclusive components can leave you tied to one supplier for the life of the equipment.
    • Geographic service gaps.If the OEM’s own service footprint is thin in your region, a warranty claim or emergency repair may take longer than a local dealer relationship would.

    Distributor risks:

    • Markup stacking.On large or repeat orders, dealer margin adds up fast this is where the cost gap with factory direct becomes most noticeable.
    • Limited customization authority.Dealers can typically only configure what the OEM allows in their dealer agreement; truly custom engineering requests still have to go back to the factory.
    • Variable quality of the dealer itself.Not every distributor offers the same level of technical competence vetting the dealer matters as much as vetting the manufacturer.

    A useful gut check either way: ask who is actually designing and manufacturing the core components structural steelwork, electrical panels, hoists, gearboxes versus assembling bought-in parts under a single nameplate. That answer affects both pricing leverage and long-term parts availability, no matter which sourcing channel you use.

    A Practical Decision Framework: 5 Questions to Ask Before You Buy

    • How standard is my spec?If you need a catalog-spec crane at a common capacity and span, the customization advantage of factory direct mostly disappears go with whichever option gets you better service and faster delivery.
    • How fast do I need it installed?If a crane failure has stopped production, distributor inventory and quicker installation crews usually beat the lead time of a built-to-order direct purchase.
    • What’s my parts and service runway look like?Confirm in writing what proprietary components exist, who stocks the replacement parts, and how far the nearest qualified technician is from your facility.
    • What’s the real order volume?Single-unit buyers often do better working with a distributor’s expertise; buyers with recurring, multi-unit, or fleet-level orders typically get enough cost benefit from factory direct to justify the longer relationship management.
    • Can I verify the manufacturer’s actual capabilities?Ask for current certifications ISO 9001 and CE marking are the common baseline internationally and ask which core components are made in-house versus sourced from third parties. A manufacturer who cannot produce current certification documentation on request is one whose quality claims can’t be trusted, and asking which core components structural steelwork, electrical panels, hoists, gearboxes are designed and built on-site is a direct way to verify real manufacturing capability.

    Total Cost of Ownership

    Sticker price comparisons miss the cost that matters most over a crane’s working life: downtime. Production losses from an idle crane compound fast, and the financial stakes vary sharply by industry. A 2023 industry report found average downtime costs surging past $2 million per hour in automotive manufacturing, with general manufacturing averaging closer to $260,000 per hour.

    That number should reshape how you weigh the factory-direct-vs-distributor decision. A slightly cheaper direct purchase that takes longer to repair after a failure because parts have to ship internationally, or because the nearest qualified technician is hours away can erase its upfront savings in a single extended outage.

    This is also where commercially available components matter. Crane systems built primarily around commercial, off-the-shelf parts motors, gearboxes, VFDs, standard control stations give you more flexibility to use independent service providers and shop around for pricing, rather than waiting on a single OEM channel. The tradeoff between proprietary and commercial components affects total cost of ownership directly, regardless of whether you bought direct or through a dealer, because it determines how quickly and cheaply you can get the crane running again after a failure.

    When comparing quotes, ask both factory-direct and distributor candidates to break out:

    • Expected lead time to delivery and installation
    • Standard warranty length and what voids it
    • Parts availability and typical replacement lead time for wear components
    • Whether routine maintenance can be performed by your in-house team or requires the OEM/dealer

    A true cost comparison includes all four, not just the invoice total.

    Conclusion

    Crane procurement can be selected according to need: customization, large quantities, need technical support for the project is suitable for the original factory direct procurement, standard equipment can be quickly picked up through the dealer, enjoy local service. Procurement decisions should focus on the full life cycle value of the equipment, comprehensive quality, qualification, technology, spare parts and after-sales advantages, cost reduction and risk avoidance.

    Henan Mine Crane Crane focuses on all kinds of lifting equipment and intelligent customized solutions, serving end customers, general contractors and global dealers, providing consulting, production, logistics, installation, after-sales full chain of one-stop service, to help customers achieve safe and efficient material handling operations.
    Henan Mine CraneDiscuss your requirements ↗
  • Crane Configuration for Shipyard Final Assembly Workshops

    Crane Configuration for Shipyard Final Assembly Workshops

    Crane Configuration for Shipyard Final Assembly Workshops

    One poorly designed crane can become a bottle neck to the entire end finishing line. When you have hull sections that can weigh hundreds of tons and tolerances to the millimeter then the crane is not just an ancilliary to the production process but is the capacity bottleneck determining how quickly that yard can turn steel into a launched vessel.

    This is the stage where the risks are greatest. Block fabrication can be achieved with the assembles in separate bays (each ironically being assembled in a dry dock). But final assembly involves cranes lifting and rotating to and joining a number of huge sub-assemblies into a single hull. It involves more than one crane working together in perfect harmony,  over what is inevitably an immense dry dock or slipway. If this experiment fails, components worth millions will be damaged.

    This brochure is a detailed explanation of the parameters, crane types, and site factors that are applied in defining cranes for the final assembly workshops not the mortiing general shipyard cranes, but those geared toward hull erection.

    What Is Crane Configuration in Shipyard Final Assembly?

    Crane specification involves selecting a crane‘s structural design, lifting gear and control system to suit the particular requirements of a workshop‘s lifting applications.  On a shipyard, it involves selecting and specifying a crane‘s capacity, span, lifting height, trolley arrangement, duty class and safety arrangements, in order that the machine can safely and reliably lift and mate hull sections, lift and place large equipment and do the necessary final pre-launch tasks.

    Final assembly set-up is not particular to crane selection. The load is not like a standard component symmetrical and balanced. Hull blocks are irregular in shape, extremely heavy and very sensitive to the introduction of eccentric forces during lifting. This requires a crane that offers both the highest capacity and the highest level of precision in positioning, a combination unusual in the world of industrial lifting.

    Why Final-Assembly Workshops Have Unique Crane Requirements

    The hull section building workshop will complete the processing of deck, bulkhead, side and other independent hull sections one by one.There is an essential difference in the mode of operation of the hull assembly workshop: the workshop transfers all completed hull sections and assembles them into complete and coherent hulls, most of which are carried out in dry docks or berths.

    The difference in operation mode makes three key changes in crane operation requirements:

    1. Synchronous lifting of multiple large components.Bow section, stern section and engine room module often need to be hoisted in sequence or in parallel, which requires multiple cranes to work together without interference.
    2. Assembly tolerance standards have been significantly tightened.Relying on programmable logic controller and frequency conversion speed regulation system to realize multi-lifting point synchronous lifting, the synchronous accuracy of lifting trolley and each lifting point can reach millimeter level, and the overall accuracy can be controlled within 3 mm or less.With this high precision, the two sections of the hull can be welded accurately without rework.
    3. The workshop undertakes the single heaviest lifting task in the whole shipbuilding process.After the main structure of the hull is closed, the crane shall hoist the heavy marine equipment such as main engine, generator set and boiler to their original positions, and hoist and lay the superstructure modules onto the deck at the same time.

    Based on the above characteristics, shipyards generally allocate cranes with the largest tonnage and the highest degree of automation to the final assembly process, while light lifting equipment is reserved for the section production and outfitting processes.

    Core Crane Types for Final Assembly

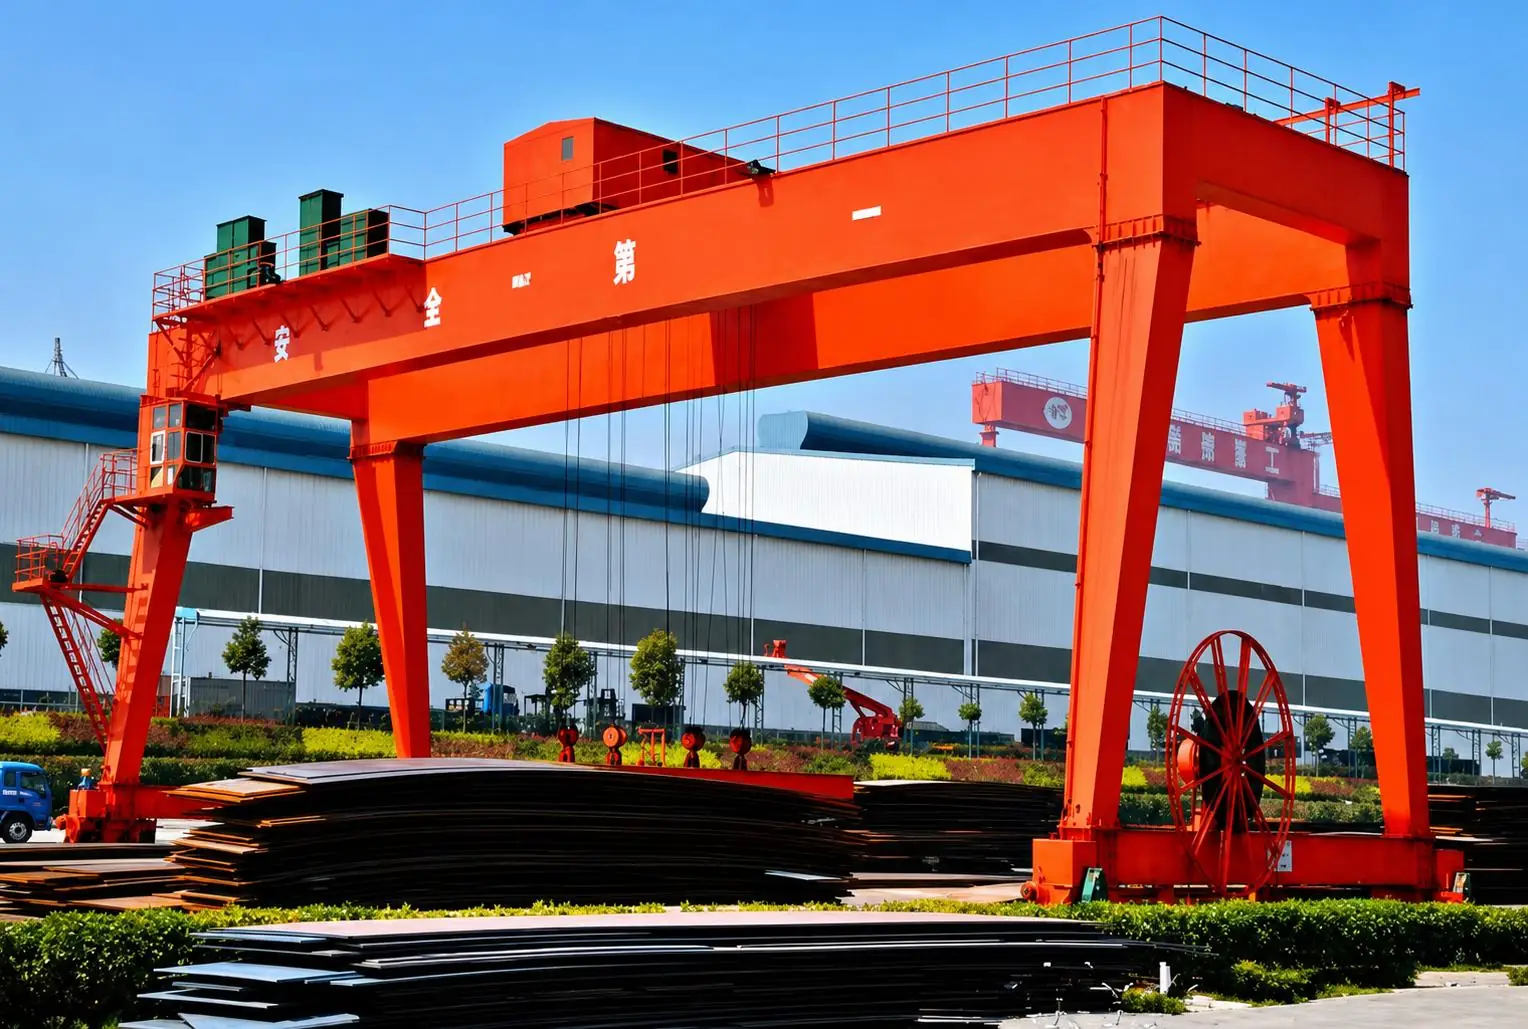
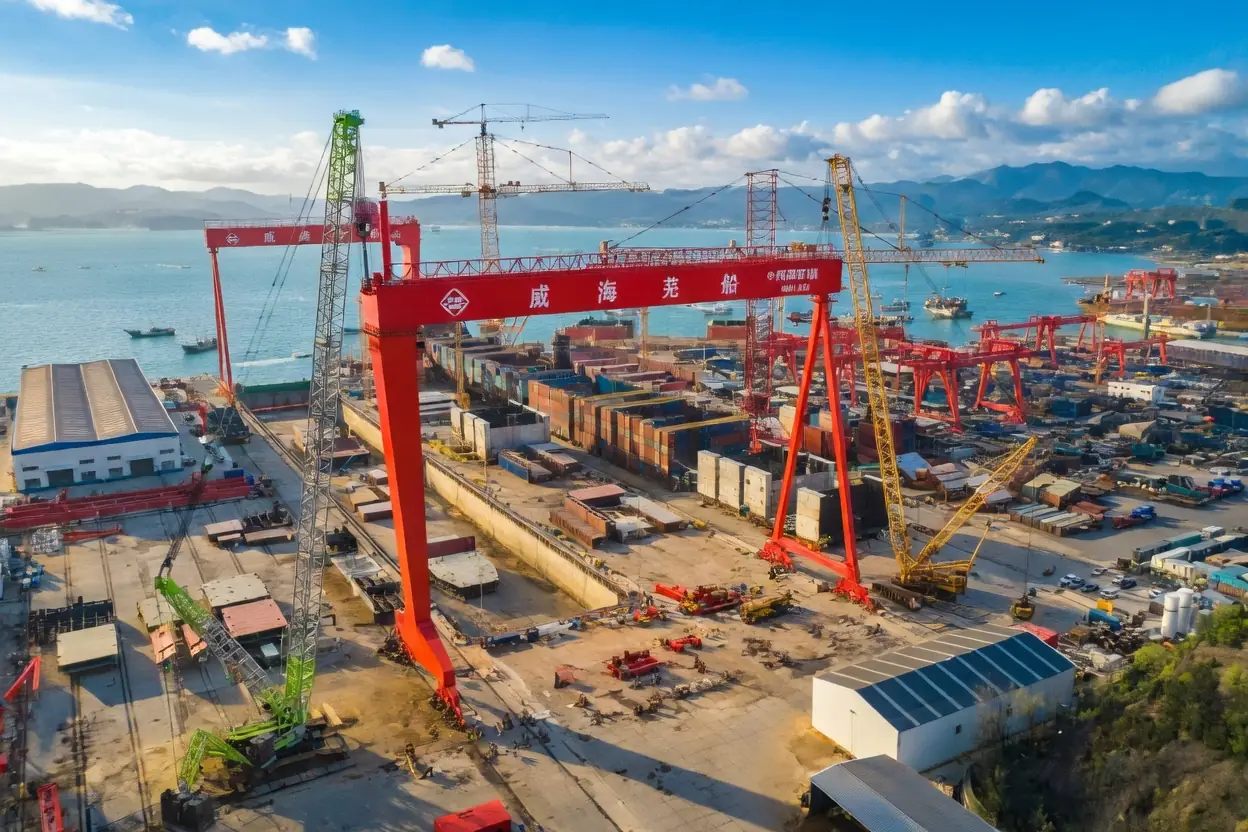
    The vast majority of shipyards use gantry cranes (also often called giant gantry cranes) to carry out hull assembly operations. The specific equipment configuration will be flexibly adjusted according to the size of the shipyard and site layout.

    • Rail gantry crane (RMG) and tire gantry crane (RTG): Among them, rail gantry crane is the standard equipment of fixed dry dock assembly station; tire gantry crane is suitable for shipyards that need to adjust the lifting path according to different projects.
    • Single beam gantry crane and double beam gantry crane: light operation in assembly workshop, including lifting of small components, tooling equipment and small modular prefabricated parts. Single beam gantry crane with smaller load specification can be selected; double beam gantry crane has stronger structural bearing capacity, which can meet the super-tonnage lifting requirements of heavy hull sections and adapt to high-intensity assembly operations.
    • Top-mounted gantry crane and down-mounted gantry crane: the lifting trolley of the top-mounted gantry crane is mounted on the top rail of the main beam, with larger bearing tonnage and wider operation span, which is the mainstream model of hull assembly operation; the down-mounted gantry crane has limited bearing capacity and is more suitable for workshop light lifting operations, rarely used for large hull assembly process.
    Configuration Factor Typical Final Assembly Choice Why
    Crane type Double-girder gantry (Goliath) Handles hundred-ton+ hull sections
    Rail system Rail-mounted (RMG) Fixed dry-dock/slipway geometry
    Trolley arrangement Dual upper/lower trolleys or multi-hook Enables synchronized, balanced lifts
    Capacity range 100–600+ tons (up to 2,000t for mega-yards) Matches block and equipment weight
    Control system PLC + VFD synchronized control Millimeter-level alignment accuracy

    Key Configuration Parameters to Specify

    Before purchasing inquiry crane equipment, the assembly workshop needs to clarify the five core selection parameters. The specific requirements are as follows:

    1. Safe Working Load (SWL): It shall be determined according to the maximum single-stage lifting weight or multi-lifting point combination lifting weight in the shipyard planning operation, and shall not only be based on the average load of current routine operation.
    2. Operation span: crane track center spacing shall completely cover the full width range of dry dock or berth, and be compatible with the temporary stacking and operation staging areas on both sides of the hull to ensure that there is no space for lifting operations.
    3. Lifting height: The effective lifting height shall be higher than the total height of the highest superstructure module and sling, and safety margin shall be reserved at the same time to meet the operation requirements of sling displacement and accessory disassembly during hull section turnover and attitude adjustment.
    4. Work level: assembly cranes need to work continuously in multiple shifts and carry large loads for a long time. Therefore, heavy operation conditions are generally adopted. The common industry standard is A7-A8, which can adapt to high-frequency and heavy-duty assembly lifting work.
    5. Trolley and lifting point configuration: single lifting point configuration is suitable for the routine operation scenario of small and medium-sized shipyards; for large special-shaped hull sections, due to the need for multi-point decentralized lifting, double trolley or multi-lifting point collaborative lifting system is the industry standard configuration, which can effectively distribute the load and ensure stable lifting and uniform force of components.

    The selection of these five core parameters is very important, among which the safe working load and working span are the most critical.  If the parameter selection is wrong, it will either result in insufficient crane load and span to undertake future large-scale ship construction projects; or it will result in excessive redundancy of equipment parameters and greatly increase unnecessary costs for equipment procurement, operation and maintenance.

    Multi-Hook & Multi-Trolley Synchronization

    Among all the parameters, lifting point and trolley configuration are the most easy to appear inadequate specification selection, and they are also the core parameters that directly affect the hull assembly quality.

    This is also the core reason why high-quality shipbuilding gantry cranes must be equipped with synchronous control systems, which can achieve stable and accurate coordinated operation of multiple lifting points, effectively ensuring the structural integrity and construction assembly accuracy of hull components.

    In actual equipment selection, the following configuration requirements shall be specified:

    • Equipped with PLC global synchronous control system, it can realize coordinated control of all trolleys and all lifting points, get rid of the limitation of traditional two-point pairing, fully adapt to the complex working conditions of multi-point synchronous lifting of large hull sections, and ensure the consistent height of each lifting point;
    • The lifting and traveling mechanism is fully equipped with variable frequency drive system (VFD), which can realize stepless speed regulation and accurate speed matching under the condition of load dynamic fluctuation, effectively avoid the running speed deviation of different mechanisms, and continuously guarantee the stability and synchronization accuracy of the lifting process;
    • Set exclusive micro-speed alignment function, which can realize centimeter-level low-speed accurate alignment fine adjustment before hull section welding, eliminate docking deviation, and greatly improve assembly accuracy and assembly quality of hull assembly;
    • Integrated anti-sway and deflection automatic correction system, can effectively inhibit the lifting load swing and component deviation during long-span walking, offset the adverse effects caused by outdoor wind disturbance, and significantly improve the safety and stability of large lifting operations.

    For shipyards adopting double-crane technology, synchronous control requirements are no longer limited to the control system of single equipment, but also need to realize cross-crane communication linkage between two cranes.  This function shall be confirmed with the supplier in advance at the equipment configuration stage, and it is strictly prohibited to reserve it for later supplement and transformation at the field commissioning stage.

    Structural & Site Considerations

    Crane configuration doesn’t happen in isolation from the workshop itself. Three site factors shape what’s structurally possible:

    Wheel loads and runway design

    A larger model crane gives a proportionately larger point load into the rail runway. The workshop foundations and rail structure should be designed or checked to resist the addition of the maximum wheel loads (under full load) of the intended crane,  and not just the weight of the crane itself.

    Workshop layout and clearance

    Span and height to under hook should encompass the entire footprint of block staging, not merely its ultimate assembly zone. Dry-dock cranes that design to span too little often lack the capacity to stage the next project‘s largest blocks as the current build progresses.

    Future capacity headroom

    Since the beneficial working life of the shipyard gantry cranes is measured in decades to the end of their service life, a typical and very expensive error would be to define a configuration precisely suited to the largest project in the present day with no allowance for growth.

    Environmental & Safety Protection

    Most shipyards are built adjacent to sea areas, and lifting equipment is always in severe marine conditions of strong wind, rainfall, high humidity and high salt fog. The gantry crane for hull assembly has large span, open-air operation and exposed structure, so it must be equipped with protective facilities suitable for marine environment. The specific requirements are as follows:

    • Marine grade anticorrosive material and special anticorrosive coating are adopted, matched with sealed electrical cabinet and stainless steel fasteners, which can resist long-term salt spray corrosion and ensure long-term stable service of equipment for decades;
    • Equipped with a complete wind protection system, including rail clamp, storm brake and wind speed linkage alarm device.  Long-span gantry crane is affected by wind load significantly, and the system can effectively avoid potential safety hazards caused by strong wind weather.
    • Equipped with parking and fastening device of the whole machine, the crane can be firmly locked and fixed when the equipment is idle and encountered strong convective gale weather, so as to prevent the risk of equipment displacement and overturning;
    • Match the operating temperature range for extreme climates. For shipyards with large temperature difference between cold and summer, cranes should meet the stable operation requirements of temperature fluctuation in all seasons, and should not only adapt to the normal moderate temperature range.

    Omitting environmental protection configuration in order to reduce initial purchase cost is the most common hidden loss mistake in shipyard crane purchase. Under coastal conditions, equipment with imperfect protection configuration is easy to corrode and age, and the subsequent high maintenance cost and shutdown delay loss will far exceed the purchase cost saved in the early stage in just a few years.

    Automation & Control Systems

    In addition to the core synchronous control performance, modern hull assembly cranes are increasingly focused on optimizing operational efficiency and safety control capabilities, with a number of intelligent and safe configurations as standard, as follows:

    • Equipped with cab operation console or remote control terminal and equipped with HD camera monitoring system, it can eliminate visual blind area in large-scale sectional hoisting process, enable operators to master the working conditions of hoisting operation area in real time and all-round way, and ensure that there is no dead angle in hoisting vision.
    • Equipped with load monitoring and overload protection system, it can identify abnormal lifting conditions in real time, warn unsafe operation conditions in advance, and avoid safety accidents such as equipment structure damage and component falling caused by excessive load from the source.
    • Integrated fault diagnosis and equipment status monitoring function, for multi-shift, heavy-duty continuous operation of crane equipment, can monitor the loss and operation status of each component in real time, provide accurate data support for maintenance team, realize preventive maintenance, and prolong the service life of equipment.
    • Push key operation data such as wind speed and load status to operators in real time, and set up direct communication channel with hull assembly construction personnel below, so as to realize up and down linkage and information exchange and avoid cooperative operation risks.

    For shipyards with multiple assembly stations, the operating data of all cranes can be consolidated into a central monitoring system.  The system can display the on-duty status, operation status and maintenance status of each equipment in real time, which is convenient for management personnel to reasonably coordinate scheduling, optimize construction scheduling, and greatly improve the overall construction operation efficiency.

    How to Configure a Crane for Your Workshop: A Step-by-Step Framework

    When the shipyard customizes and purchases the final assembly crane, it is necessary to confirm the parameters and working conditions item by item according to the standardized process to ensure that the equipment fully meets the construction requirements. The specific implementation points are as follows:

    1. Check existing and future maximum lifting loads: calculate the weight of maximum hull sections, main equipment and superstructure modules, and include the weight of lifting tools and rigging to verify the required safe working load (SWL) of equipment.
    2. Geometric size of survey workshop site: actual measurement of effective width of dry dock and berth, determination of required operation span of crane; measurement of stacking height of highest component on site, verification of effective lifting height of hook in combination with assembly requirements.
    3. Clarify the working condition grade of equipment: count the lifting frequency of single shift, the average proportion of conventional operation load to rated load, and accurately determine the required working grade of crane according to the actual operation intensity.
    4. Determine the configuration scheme of trolley and lifting point: match the configuration of single lifting point, double trolley or multiple lifting points according to the shape size and structural weight of conventional hull sections of shipyard; at the same time, complete the selection by adopting double-crane combined lifting technology according to whether it is normalized.
    5. Clarify the synchronization control accuracy index: set the alignment accuracy standard required for hull section closure (the mainstream standard for ship assembly is millimeter accuracy), verify that the crane control system can stably meet the standard and meet the requirements of high-precision assembly.
    6. Matching marine environmental protection parameters: according to the coastal salt fog, strong wind, temperature and humidity and other climatic conditions of the plant, the anti-corrosion coating grade, windproof configuration and equipment temperature resistance interval are determined according to the plant, and the severe sea conditions are adapted.
    7. Verification of site structure bearing conditions: confirm the bearing capacity of crane track beam and civil foundation, which can fully match the wheel pressure load under full load state to ensure the safe operation of equipment.
    8. Submit to the manufacturer for professional verification: before the quotation is finalized, qualified equipment manufacturers are required to conduct special verification and confirmation on wheel pressure parameters, drive configuration and main structure strength in combination with berth layout and local wind zone grade.

    Choosing a Supplier or Partner

    Not all crane manufacturers have the R & D and manufacturing capabilities of large-scale synchronous lifting equipment in shipyards. Compared with ordinary industrial cranes, such equipment is more professional and has higher technical threshold.  When shipyards select cooperative suppliers, they shall focus on verifying the following core conditions:

    • Practical operation experience of the same tonnage project: the supplier is required to provide the past landing cases with the same tonnage or higher than the demand of the factory, and the manufacturers with large-span and heavy-duty shipbuilding crane manufacturing experience are preferred.
    • Autonomous core synchronous control technology: PLC frequency conversion synchronous control system is the core key of hull assembly crane, not a universal add-on accessory, requiring manufacturers to have independent R & D, debugging and optimization of the core technical capabilities.
    • Complete machine pre-installation and factory test capability: regular manufacturers will complete machine pre-installation, component debugging and performance testing before the equipment leaves the factory, which can greatly reduce the failure risk and construction period pressure of on-site installation and debugging.
    • Customized site engineering supporting services: wheel pressure, drive system and main structure parameters can be customized according to the actual working conditions of dry dock and berth of shipyard, instead of applying general standard specifications.
    • Perfect after-sales and spare parts guarantee: shipbuilding gantry crane design service cycle for decades, suppliers need to have long-term stable after-sales operation and maintenance, spare parts supply and equipment upgrade service capabilities.

    Conclusion

    Accurate selection and configuration of shipyard cranes is the key to ensure long-term safe production and efficient operation and maintenance.  Scientific selection can take into account the current construction needs and future expansion and maintenance projects, and avoid later transformation and shutdown losses by checking equipment structure, accuracy and site conditions.

    Compared with general models, shipyard customized lifting equipment is more adaptable.  Customized design and full-process service from professional manufacturers can optimize equipment performance, reduce life-cycle costs and enhance long-term use value.

    Henan Mine Crane focuses on the R & D and manufacturing of heavy lifting equipment. It can provide customized lifting equipment and intelligent lifting system for ships, marine engineering and other scenarios, supporting site survey, structure verification, customized design and other complete technical services to create safe and efficient lifting solutions.

    Henan Mine CraneDiscuss your requirements ↗
  • Container Yard Planning & Capacity Calculation | Equipment Solutions

    Container Yard Planning & Capacity Calculation | Equipment Solutions

    Container Yard Planning & Capacity Calculation | Equipment Solutions

    To do container yard planning, many people’s first reaction is to figure out how many boxes can be placed on a piece of land.However, in actual operation, it is often encountered that the theoretical capacity is enough, but the actual situation is blocked. The truck queues up, the containers are frequently reversed, the equipment cannot be turned around, the land and equipment are not put into less investment, but the throughput cannot go up.
    The actual storage yard capacity is never simply divided by the area of a single box covers an area of, it and stacking height, box structure, equipment selection, operation channel, storage cycle, peak fluctuations are directly related.As a manufacturer of port yard equipment, Henan Mine Crane has come into contact with many projects that are full in planning stage and crowded in operation stage.This article explains the complete logic, core formula, influencing factors and equipment matching method of capacity calculation clearly, and helps the customers who build or expand the storage yard to make solid preliminary planning.


    What is the container yard capacity

    In short, container yard capacity refers to the number of containers or total TEU that can be stored at the same time in a site under the premise of safe and smooth operation, as well as the corresponding annual throughput capacity that can be carried.
    The static capacity depends on the simultaneous storage capacity, and the dynamic annual throughput capacity shall be calculated in combination with the average storage period of containers.The basic algorithm commonly used in the industry is to multiply the number of ground container spaces by the average stacking height, and then multiply by the TEU conversion factor and the actual utilization rate to obtain the static container storage capacity; and then combine with the average stacking days to convert the annual processing capacity.
    A lot of planning mistakes are based on 100% full load calculation, ignoring the passage, safety spacing, special box area, equipment operation space and operation buffer, and finally the actual usable capacity is far lower than the theoretical value.

    Why is capacity planning important

    The capacity of the storage yard directly determines the upper limit of the overall throughput of the wharf.If the configuration of quay crane, gate and truck is sufficient, the yard cannot be connected or rotated, and the whole link will be blocked in the middle.A complete container terminal capacity is the result of the matching of berth, yard and gate. It is useless to look at one item alone.
    Capacity planning also directly determines equipment selection.Different handling equipment corresponds to a completely different stacking density, with RTG rubber-tyred gantry cranes having the highest stacking density, front cranes requiring more turning and working space, and straddle carriers lying in between.If the equipment is not selected correctly, either the land is wasted seriously, or the operation efficiency is not improved.
    The hidden costs brought about by unreasonable planning are higher: the number of container dumping increases, the waiting time of the truck increases, the fuel consumption increases, the equipment idling increases, and the potential safety hazards brought about by the yard congestion are not small expenses in the long run.

    Capacity Characteristics of Stockyard Corresponding to Different Equipments

    Equipment Type Stacking Density Space Requirement Best Application Scenario
    RTG Crane High Medium (planned blocks) Large high-density container yards
    RMG Crane Very high Low (fixed rail layout) Rail terminals & automated yards
    Reach Stacker Medium-high High (turning radius needed) Small & medium yards, ICDs
    Straddle Carrier Medium Medium (traffic lanes) Flexible terminal-wide operations
    Empty Container Handler Very high Medium Empty container storage yards

    Clear up a few core concepts before calculating

    Before calculating the capacity, align a few basic concepts so that the result will not deviate too much.
    TEU is also the standard container unit, 20 feet container is 1 TEU, 40 feet is 2 TEU, 45 feet is usually 2 TEU for planning conversion.The total TEU capacity of a storage yard varies significantly with the proportion of container types.
    Ground slot refers to the position on the ground where a standard container can be placed.If the site is planned as per 40-foot container space, it shall be converted into unified TEU unit for calculation and then summarized.
    Stacking height is how many layers can be stacked in the vertical direction. In the industry, 1-over-2 means stacking 3 layers high, and 1-over-4 means stacking 5 layers high.The higher the pile, the greater the capacity per unit area, but the probability of falling boxes will also increase accordingly.
    The utilization ratio of the storage yard is the proportion of the theoretical capacity that can be used normally.In reality, it is impossible to fill up 100%, so the truck passage, equipment walking space, safety distance, refrigerator area, dangerous goods area, inspection area and operation buffer space shall be reserved.
    Stacking period refers to the average number of days that the container stays in the yard from the arrival to the departure.The shorter the stockpiling period, the greater the annual throughput that can be supported by the same static capacity.

    Calculation formula of basic capacity

    The core formula for static yard capacity is not complicated:
    Static storage capacity (TEU)= number of ground containers * average stacking height * TEU conversion factor * storage utilization
    Take an intuitive example: a yard has 1000 ground container slots, 4 layers are stacked on average, the conversion factor of TEU is 1.6, and the actual utilization rate is calculated as 75%, so the static capacity is 1000 × 4 × 1.6 × 0.75 = 4800 TEU.
    Among these parameters, stacking height and utilization rate are the most likely to be overestimated.The stacking height shall match the equipment capacity, and the utilization rate shall be determined in combination with the functional partition of the storage yard. The more complex the function of the storage yard, the lower the actual utilization rate.

    The conversion of annual throughput capacity also has the corresponding formula:

    In the yard throughput capacity = static capacity x 365 present the average storage period
    Again, if the average storage period is 6 days, the throughput is 4800 x 365/6 = 292000 TEU/year.
    This also shows that shortening the storage period of containers is an effective way to improve the throughput capacity without expanding the land.
    The reverse can also be extrapolated: given the annual throughput target, calculate how many ground slots are needed.The formula is:
    The number of ground slots required = TEU amount x average storage period x peak factor present 365 present average stack height present utilization rate present TEU coefficient
    For example, the annual target is 200,000 TEU, the average stacking time is 7 days, the peak value coefficient is 1.2, the stacking is 4 layers, the utilization rate is 75%, and the TEU coefficient is 1.6, so about 960 ground container slots are needed.

    Core Factors Affecting Yard Capacity

    Calculate the theoretical value, but also combined with the actual situation to do correction, there are several factors that have the greatest influence.
    The first is the total area and layout of the yard.In the total available land, the box area only accounts for a part, and the area of truck collection road, equipment walking area, fire escape, maintenance site, gate entrance and exit, and railway connection area shall be deducted.The land utilization rate varies greatly with the arrangement of the box area.
    The second is the box structure.The proportion of 20 feet, 40 feet, empty containers, refrigerated containers, dangerous goods containers, transit containers, will change the actual capacity.The refrigerator shall be connected with electricity, maintenance passage shall be reserved, and the dangerous goods box shall be kept with safe spacing, which occupy more space than the ordinary dry box.
    The effects of the stockpiling period are most easily overlooked.The same static capacity, storage period of 3 days and storage period of 10 days, the annual throughput can be more than three times.Different business modes lead to great differences in stacking period, with short stacking period at transit port and long stacking period at inland bonded yard.
    Stacking height is not the higher the better.The higher the pile, the greater the theoretical capacity, but the number of cases will increase, the single box operation time becomes longer, the actual operation efficiency may decline.To match the equipment capacity, box area management level.
    The impact of equipment type has also been mentioned above. RTG and RMG have high density, and the front crane and forklift require large working space.The same piece of land, choose different equipment, available capacity and operating efficiency are completely different.
    There are also peaks and seasonal fluctuations.It is not only calculated according to the average daily quantity. In peak season, when ships arrive at the port intensively and the suitcase is delayed, the pressure on the storage yard will increase sharply.Generally, the peak coefficient of 1.1 to 1.5 shall be reserved, otherwise it is easy to block during peak period.

    Common Calculation Mistakes

    Planning stage is the most easy to step on a few pit, a lot of yard are met.
    Calculating capacity at 100% utilization is the most common mistake.It’s really full, vehicles can’t get in, equipment can’t turn on, normal operation can’t be carried out at all, which is equivalent to man-made congestion.
    Only static storage capacity is calculated, and the impact of storage period on throughput is not considered.Two static capacity of the same yard, storage period is different, the annual processing capacity.
    Ignore equipment turning radius and working space.Especially for the storage yard with front crane, there is not enough turning depth and operation depth left, the equipment cannot be used, and the actual available container spaces are much less than planned.
    Do not distinguish between box type, according to the ordinary dry box.There are a large number of refrigerated containers, dangerous goods container yard, but also according to the ordinary standard calculation, the final capacity is certainly not enough.
    It’s just storage, not circulation.The storage yard shall be matched with the quayside crane capacity, gate capacity, truck capacity and equipment operation efficiency, and it is meaningless to look at the number of containers stored.

    how to change that capacity of storage yard by equipment selection

    Different loading and unloading equipment, the capacity of the yard to shape the logic is completely different.
    The front crane is suitable for small and medium-sized storage yards, inland storage yards and railway stations, with strong flexibility and low investment, but it needs more space for driving and turning, and the storage density is not as good as that of the gantry crane system.
    RTG rubber-tyred gantry crane is suitable for high-density container area operation of medium and large storage yards, with neat stacking and high density, which is the mainstream choice of large terminals, but it needs regular container area layout and higher initial investment.
    RMG rail-mounted gantry crane has higher density and low electrification operation cost, which is suitable for railway station and automatic storage yard. The disadvantages are fixed track, poor flexibility and large investment in early infrastructure.
    Straddle carrier gives attention to both transfer and stacking, flexible operation, suitable for the need to transfer the wharf, but the stacking density than gantry crane equipment.
    Special equipment for empty containers can be stacked very high, and special equipment for empty container yard can greatly improve storage density.

    Method for increasing capacity without expanding land

    Land tight yard, don’t rush to expansion, several directions can tap the potential.
    The most effective way is to shorten the stacking period. By means of booking containers, quick customs clearance, optimizing truck scheduling and electronic container placement, the containers can be transferred faster, and more containers can be handled in the same site.
    Optimize the layout of the yard, adjust the arrangement of container areas, lane direction and position of special container areas, reduce cross moving lines and invalid space, and squeeze out a lot of available capacity.
    Replace higher density work equipment, such as upgrading from a front hoist to an RTG, increasing stacking height and box area density, and increasing storage capacity on existing sites.
    Empty container and heavy container partition management, empty container with special equipment stack is higher, heavy container area optimization box logic, each play a maximum efficiency.
    Make good use of the terminal operating system TOS, reduce unnecessary box turnover, improve the accuracy of box position, and also improve the effective capacity and operation efficiency in a disguised form.
    Finally, we must leave enough peak buffer, do not use up the site according to the average daily volume, otherwise the peak season will be congested.

    common problem

    What is the formula for calculating the capacity of the container yard?

    Static capacity = number of containers on the ground × average stacking height × TEU conversion factor × yard utilization rate; annual throughput capacity = static capacity × 365 ÷ average stacking period.

    What is the difference between static capacity and throughput?

    Static capacity is how many containers can be stored at the same time, and throughput capacity is how many containers can be handled in a year, and the latter is directly related to container residence time.

    Yard utilization rate generally take how much more reasonable?

    Planning is not calculated at 100%, to set aside lanes, equipment operation space, safety zone and peak buffer, most of the yard between 65% and 80%, the more complex the function value is lower.

    What equipment can lead to higher yard capacity?

    RTG and RMG gantry cranes have a higher stacking density; front cranes are more flexible but require more working space.

    How to improve the throughput capacity of the storage yard without expansion?

    Shortening the stacking period, optimizing the layout, improving the stacking density, upgrading the equipment and optimizing the management of the box area can improve the throughput capacity on the existing land.

    epilogue

    It is not as simple as setting a formula to calculate the capacity of container yard clearly, but comprehensively judge in combination with many factors such as container type, equipment, stacking period, peak value, moving line, etc.Reasonable planning can not only improve the land utilization rate, but also reduce the dumping and congestion, so that the equipment and site can play their due value.

    Customize Your Solution

    As a professional supplier of port yard equipment, Henan Mine Crane can provide the whole process service from yard planning, equipment selection to scheme implementation.If you are planning to build a new storage yard or evaluating the capacity expansion potential of the existing storage yard, you can send us the site area, annual TEU target, average storage period, box structure and intended equipment, and the engineering team will help you calculate the reasonable capacity configuration and recommend the matching handling equipment scheme

    Henan Mine CraneDiscuss your requirements ↗
  • Container Yard Equipment Buying Guide

    Container Yard Equipment Buying Guide

    Container Yard Equipment Buying Guide

    To do container yard planning, equipment selection is a link that affects the whole body.
    If you choose the right equipment combination, the land utilization rate, truck turnover speed, and long-term operating costs can all be within a reasonable range; if you choose the wrong one, either the storage capacity cannot keep up with business growth, or the on-site congestion and container dumping are frequent, and subsequent renovation and expansion will cost you a lot of wasted money.
    When many purchasers make planning for the first time, they tend to focus only on the quotation of single equipment for comparison, ignoring the more critical factors such as yard layout, throughput rhythm, box structure and future expansion. As a manufacturer of deep-ploughing port loading and unloading equipment, Henan Mine Crane has been exposed to hundreds of yard projects, large and small. This guide clearly explains the adaptation scenarios, selection logic and pit avoidance points of mainstream equipment, and helps you build a yard equipment combination suitable for your own needs.


    Quick Selection Reference

    First, give a direct judgment conclusion to facilitate quick scene matching.
    Small inland storage yard and logistics park, container front crane plus dock tractor is a combination of high flexibility and low input threshold; high-density large container storage yard, RTG tire gantry crane or RMG rail gantry crane is preferred, stacking density and operation efficiency are more advantageous; the terminal that needs full-field flexible transfer and stacking, clearing quay crane waiting, container straddle carrier adaptability is stronger; The storage yard with high empty container ratio, equipped with special empty container stacker, is more cost-effective than heavy equipment to deal with empty containers.

    Core characteristics of mainstream yard equipment

    RTG rubber-tyred gantry crane

    RTG is a door-type lifting equipment that runs on rubber tires. It mainly focuses on container stacking operations in the FCL area. The conventional model span can cover 6 to 8 rows of containers plus a collection truck lane, and the stacking height varies from 1-over-3 to 1-over-6. It is the core equipment for improving the land utilization rate of medium and large storage yards. There are diesel, hybrid and pure electric power options.
    It is suitable for medium and large container yards, inland ports with expansion plans, and sites seeking high storage density. The advantages are high stacking density, regular box area, large automatic transformation space, and lower single box operation cost under large throughput scenario.
    The limitation is that the initial investment is higher than that of the front crane, the storage yard needs to make regular box area planning in advance, and the flexibility of long-distance horizontal transfer is general, usually with dock tractor for horizontal transfer.
    Before purchasing, check clearly: span requirements, stacking layers, power type, automation level, rated load, anti-sway and alignment configuration, box lane width.

    RMG rail-mounted gantry crane

    RMG runs along fixed tracks and is mostly used for high-density stacking operations in ports, railway stations and automated storage yards. It can customize different spans and stacking heights according to needs. The electrified operation cost is low. It is the mainstream selection of automated storage yards.
    It is most suitable for railway container center station, multimodal transport yard, automatic container terminal and other fixed layout scenarios. The advantages are extremely high stacking density, high stability and accuracy of operation, and the greatest potential for automatic upgrading.
    The limitation is that there is no flexibility in track fixation, high requirements for infrastructure construction, higher planning and installation costs in the early stage, and almost no space for adjustment in the box area in the later stage.
    When purchasing, confirm: track span, stack height requirements, cantilever configuration, track foundation conditions, power supply mode, automation level, docking size with railway cars/collection trucks.

    container reach

    Front sling telescopic boom and special sling, is a very versatile mobile loading and unloading equipment, rated lifting capacity of about 45 tons, in addition to standard containers, replacement of accessories can also handle special containers and miscellaneous Kalmar
    It is the preferred main equipment for small storage yards, inland container yards (ICD), railway stations, logistics parks, and is also suitable as an auxiliary supplement for large storage yards. The advantage is that it is extremely flexible, almost no additional infrastructure is needed, it can be used on approach, the initial investment is low, the narrow space can also be operated, and loading and unloading and short-distance transshipment can be considered.
    The limitation is that the dumping rate is high in high density stacking, the operation efficiency is not as good as that of gantry crane in large throughput scenarios, and the tire loss and fuel cost ratio are not low.
    Purchase to check: heavy load/empty container operation positioning, rated lifting weight, stacking layers, operation depth, site load, adaptation box type, power type, equipment requirements.

    straddle carriers

    Straddle carrier is a door-type self-propelled equipment, which can lift containers under the frame. Single equipment can independently complete the whole process of taking containers, transferring and stacking without additional lifting equipment. The stacking height is usually 1-over-2 to 1-over-3Konecranes.
    It is suitable for medium-sized terminals with complex moving lines and flexible transshipment throughout the site, as well as scenarios where you want to eliminate the waiting time for the connection between the shore crane and the yard. The advantage is that it integrates hoisting and horizontal transfer, flexible scheduling in the whole field, can reduce the waiting loss of different equipment connection, and can adapt to irregular sites.
    The limitation is that the whole team procurement investment is not low, the traffic management in the field is more complex, the storage density is not as good as the gantry crane system, and the requirements for operators are higher.
    Procurement shall confirm: stacking height, power type, automation level, average haul distance per trip, number of equipment required to match quay crane efficiency, lane planning, maintenance team capacity.

    Wharf tractor and empty container stacker

    Wharf tractor is mainly used for towing chassis within the yard for short distance, and it is necessary for most regular yards to complete horizontal transfer with gantry crane. It has low cost and flexible deployment.
    Empty container stacking machine is specially designed for empty container stacking, with strong stacking capacity, high operation efficiency, procurement and operation costs much lower than heavy load front crane, suitable for leasing stations and container repair areas with large empty containers.

    Container Yard Equipment Selection Matrix

    Buyer Scenario Recommended Equipment
    New small inland container depot Reach stacker + terminal tractor
    Large high-density container yard RTG crane
    Rail intermodal terminal RMG crane + reach stacker
    High empty container volume Empty container handler
    Flexible container transport across yard Straddle carrier
    Limited initial budget Reach stacker
    Limited land area RTG or RMG crane
    Fast trailer shunting Terminal tractor
    Future automation plan RMG / automated RTG / electric tractor
    Mixed cargo & container handling Reach stacker
    Low-emission port project Electric RTG / electric tractor
    High truck congestion Optimized tractor fleet + RTG/RMG system

    Core logic of selection

    The type and size of the storage yard shall be clarified first. The optimal equipment combination is completely different for different scales and attributes of storage yard. For small inland storage yard and dry port logistics park, the combination of front crane and tractor with high flexibility and low infrastructure requirements shall be preferred; medium storage yard can be upgraded to RTG according to the container volume; large hub port, railway central station, RMG or RTG plus tractor combination can exert scale effect.
    Calculate the true throughput requirements. Do not only look at the total annual container volume, but also dismantle the daily average volume, peak container volume, import and export ratio, average storage period, and the law of truck collection to port. The dynamic storage capacity is directly related to the storage period. The shorter the storage period, the larger the annual throughput supported by the same static capacity. Equipment selection should match the peak operation demand, not only according to the daily average quantity.

    Match the objective conditions of the site.

    For sites with tight land, RTG or RMG shall be given priority, and capacity shall be changed by high stacking; for sites with irregular shape and frequent adjustment of box area, flexible equipment such as front crane and straddle carrier shall be selected; for storage yards with railway access, RMG or front crane shall be given priority to meet railway loading and unloading requirements.
    Calculate the full cycle cost, not just the purchase price. Single unit purchase price from low to high is roughly: dock tractor, empty container stacker, front crane, straddle carrier, RTG, RMG and automation system. However, the capital construction cost and operation cost vary greatly. To analyze the total cost of ownership of storage yard equipment, the purchase, capital construction, energy consumption, maintenance, labor and shutdown losses should be included, and the real cost comparison can be obtained only if they are calculated according to the 10-year cycle.
    It is also necessary to select the appropriate energy type, check the safety compliance requirements, examine the supplier’s after-sales and spare parts support, and reserve room for future upgrades. The downtime loss of yard equipment is much higher than the maintenance cost, and reliable after-sales and spare parts supply is more valuable than small discounts at the time of purchase.

    Common purchasing mistakes

    Staring only at the purchase price is the most common pit. Low-cost equipment often consumes high energy, has many failures, and has a slow supply of spare parts. The total expenditure is higher in the long run.
    It is also common to overlook site suitability. For example, no matter the size of the site, RTG is hard, and the box area planning is not open, and the equipment cannot be used; or the ground bearing is not considered, and the site settlement deformation is caused after heavy equipment is installed.
    There are also blind pursuit of high stacking, only to see the theoretical capacity, ignoring the higher the stack, the more the box, the actual efficiency of the operation will decline.
    Do not value after-sales support, until the equipment failure can not find repair, only to find that the downtime loss is much greater than the original purchase price difference.

    FAQ

    What equipment is most suitable for small storage yard?

    Small inland storage yard or logistics park, front crane and dock tractor is the most practical combination, low investment, fast deployment, flexibility, can meet the needs of loading and unloading and short-distance transfer at the same time.

    What equipment should be selected for high density storage?

    RTG and RMG gantry cranes are more suitable for high density storage, regular container area, high land utilization, suitable for medium and large fixed storage.

    What is the difference between RTG and RMG?

    RTG runs on rubber tires and has a more flexible layout;RMG runs along fixed tracks with higher stacking density and more stable operation, suitable for fixed layout storage yards and railway stations.

    epilogue

    In general, there is no absolute best equipment, only the combination that best suits its own scene. The model selection shall be based on the comprehensive judgment of yard scale, throughput demand, site conditions, budget planning and long-term development, and the account shall be calculated to the whole life cycle, instead of only focusing on the initial purchase price.

    Customize Your Solution

    Henan Mine Crane, as a professional custom manufacturer of storage yard equipment, can provide all kinds of container storage yard equipment, support customized configuration, and provide full-process services from scheme planning, production and manufacturing to installation and commissioning and lifetime maintenance. If you are planning yard or updating equipment, you can send us yard area, annual TEU container volume, container structure, stacking height requirements, storage period and budget range. The engineering team will help you compare the advantages and disadvantages of different equipment combinations and issue appropriate configuration schemes and cost estimates.

    Henan Mine CraneDiscuss your requirements ↗
  • Container Straddle Carrier Selection Guide | Specs, Types & TCO Analysis

    Container Straddle Carrier Selection Guide | Specs, Types & TCO Analysis

    Container Straddle Carrier Selection Guide | Specs, Types & TCO Analysis

    As the scale of global container freight continues to expand, seaports, intermodal terminals and inland logistics parks are facing the double pressure of speeding up the turnover of yards and controlling operating costs. container straddle carrier, as a tire-type handling equipment integrating lifting, transferring and stacking, has become one of the core equipments of the modern container logistics system by virtue of its flexible site adaptation capability. As a set of lifting and transferring, stacking and yards all-in-one tire handling equipment, it has become one of the core equipments in modern container logistics system by virtue of its flexible site adaptability.

    Many purchasers only focus on the load and offer when selecting the model, ignoring the parameters and the scene of the matching degree, and finally either the equipment performance can not keep up with the yard rhythm, or the configuration of the surplus caused by the waste of funds. This guide from the principle of equipment, core parameters, scene fit, selection methods, maintenance points of the whole dimensions of the dismantling, to help global ports, logistics operators to clarify the whole set of selection logic.

    What is a cross-traffic container truck

    Basic Definition

    Container transporter is a gantry structure of tire-type self-lifting equipment, the frame of the operation directly across the top of the container, through the spreader to complete the lifting and landing of the box, while relying on its own power to complete the horizontal transfer of the field. Unlike traditional gantry cranes, it does not require a fixed rail, set loading and unloading, handling functions in one, a single device can cover the whole process of the container from picking up the box to the drop.

    This type of equipment was first used in coastal ports in Europe and the United States, with the development of global multimodal transportation, gradually popularized to the railroad yard, inland yards, logistics parks, suitable for more and more rich working conditions and scenarios.

    Working Principle

    The lifting system mostly adopts hydraulic or electric drive, with special container telescopic spreader, which can be adapted to 20-foot, 40-foot, 45-foot standard ISO containers, and the lifting process is smooth and controllable.

    Walking system relies on multiple sets of rubber tires driving, divided into two speeds of empty load and heavy load, taking into account the efficiency of transfer and operational safety.

    The steering system supports multi-mode steering, including normal front-wheel steering, all-wheel steering, tilting, in-situ steering, adapting to different widths of the yard aisle, and can work flexibly in narrow spaces.

    The complete operation process is usually as follows: the equipment travels to the top of the target container → spreader alignment and locking → lifting the box to a safe height → traveling to the target stacking position → precise alignment and dropping of the box → unlocking and driving away, and the whole process is completed by a single piece of equipment independently.

    Core components

    High-strength portal steel frame is the main load-bearing foundation of the equipment, taking into account the structural strength and self-weight control, suitable for heavy-duty long-term operation.

    Lifting system includes power unit, transmission mechanism, spreader connecting frame, which is the core module to determine the lifting performance.

    Specialized container telescopic spreader can be adapted to different specifications of the box, with a rotary locking mechanism to ensure the safety of the box lifting.

    The drive system includes power unit, transmission mechanism and axle, which determines the driving and steering performance of the equipment.

    Large-size heavy-duty rubber tires can carry the weight of the whole machine and cushion the bumps on the ground at the same time, which is suitable for different hardened sites.

    Closed cab provides operators with a good view and a well-protected working environment.

    Multi-level safety system, covering anti-collision, overload, limit, emergency braking in multiple dimensions, to ensure the safety of the whole operation.

    Common Types of Container Trucks

    Diesel-powered container trucks

    Diesel model is the industry’s longest application of mature models, strong power output, to deal with heavy-duty, continuous operation of the stability of the extreme temperature, the adaptability of the bad site better.

    It is suitable for all-weather operation of large seaports and inland hubs with high throughput, and has a mature supporting maintenance system, which makes it convenient to purchase spare parts globally.

    Hybrid Container Trucks

    The hybrid model adds energy storage and recovery unit on the basis of diesel power, which recovers energy when the vehicle decelerates and the spreader is lowered, and then assists in the operation of the driving equipment, which can significantly reduce fuel consumption and exhaust emissions.

    It is suitable for medium-sized yards that want to control operational energy consumption and gradually transform to green logistics, and it can realize a certain degree of cost reduction and emission reduction without significant changes to the existing supporting facilities.

    Electric Container Truck

    The all-electric model is driven by lithium battery, with zero exhaust emission during operation, low noise, simpler power transmission structure, fewer wearing parts and lower long-term maintenance cost.

    With the tightening of carbon neutral policy in global ports, the procurement proportion of electric models is increasing year by year, which is especially suitable for logistics parks around the city and regional yards with strict environmental control.

    Automated Driverless Transporter

    The driverless model is equipped with GPS positioning, laser navigation, and cluster scheduling system, which can autonomously complete the path planning, box handling, and precise alignment without the need for operators to be on-site.

    Mainly used in automated intelligent port, large hub yard, can significantly reduce labor costs, improve the standardization of yard operations, is one of the core development direction of the future of intelligent logistics.

    Core technical parameters of container straddle carrier

    The matching degree of container straddle carrier specification directly determines the operational efficiency and service life of the equipment, and the selection should be checked item by item to meet the needs of the scene.

    Rated lifting capacity

    The mainstream tonnage of the industry covers 35 tons to 60 tons, and different tonnage corresponds to clear usage scenarios:

    • 35 tons: the main empty container stacking, light load transfer, suitable for empty container yard, logistics distribution center.
    • 40 tons: general standard model, can cover most of the full-loaded standard container operations, is the mainstream choice for small and medium-sized yards.
    • 45 tons: suitable for heavy cargo export, heavy duty container yard, more stable to deal with minerals, machinery and equipment heavy containers.
    • 50 tons and above: special customized models, for over-limit containers, heavy engineering containers and other special scenarios, tonnage selection should reserve a reasonable margin, to avoid long-term full-load operation of the equipment to accelerate the aging of the structure and components.

    Stacking capacity and lifting height

    Stacking capacity is usually labeled with “1-over-N”, 1-over-2 means that the equipment can be stacked across 1 layer, 2 layers, and so on, the mainstream configuration of 1-over-2, 1-over-3, 1-over-4 three kinds.

    The higher the number of stacking layers, the larger the storage capacity of the yard with the same floor space, and the higher the cost of land in the port area and the peripheral yard of the city, the more suitable to choose the high-level stacking model.

    The corresponding lifting height ranges from 9 meters to 13 meters. When selecting the model, it is necessary to take into account the number of stacking layers, the height of the containers, the operational safety clearance, and to avoid obstacles such as lighting and pipelines above the site.

    Traveling and steering parameters

    Mainstream models of unladen traveling speed 25-30km / h, fully loaded traveling speed 20-25km / h, the faster the speed, the higher the efficiency of long-distance transit, but also to match the safety design of the yard access.

    Wheel configuration is common 4-wheel, 6-wheel, 8-wheel structure, the larger the load, the weaker the site bearing, the more the need for multi-wheel configuration to disperse the grounding ratio pressure.

    The richer the steering mode, the stronger the adaptability to the narrow yard, all-wheel steering, in-situ steering function, can greatly reduce the vehicle turnaround to occupy the channel space.

    Other core parameters

    The self-weight and external dimensions of the whole machine should be checked with the site bearing and channel width to avoid the over-width and over-weight can’t enter the yard.

    Automation function can be optional on demand, the basic model is manual driving, can be added with remote monitoring, fault diagnosis; medium and high-end models can be equipped with semi-automatic auxiliary alignment, automatic collision avoidance; high-end models to support the full unmanned, fleet intelligent scheduling.

    Mainstream Application Scenarios of Container Transporter

    Container harbor terminal

    Coastal ports are the most core application scenarios for trans-shipment vehicles, which mainly undertake horizontal transfer of containers from shore to yard, internal stacking and finishing in the yard, and transferring of boxes before loading.

    Compared with the traditional mode of “bank bridge + container truck + yard bridge”, trans-carrier can reduce the intermediate transfer links, ease the traffic congestion inside the yard, and improve the flow speed of the whole operation chain.

    Intermodal Railway Yard

    Railroad container yards need to frequently transfer containers between railroad flatcars, yards and highway trucks. The flexible steering and moving ability of trans-carrier can quickly complete the changeover of different transportation carriers, shorten the train’s stopping time at the station, and improve the turnover efficiency of railroad trains.

    Inland Container Depot (ICD)

    Most of the inland distribution yards do not have conditions for laying heavy-duty tracks, and the advantages of cross-traffic cars that do not require track infrastructure and can operate on conventional hardened ground are very prominent. Subsequent expansion of the yard, layout adjustment, the equipment can be directly adjusted to the scope of operation, without additional investment in civil transformation costs.

    Freight distribution centers and logistics parks

    Logistics distribution centers around the city have fast container flow and short stacking cycle, and the trans-loader can quickly complete the whole process of unloading, stacking and loading, which is suitable for the demand of multi-batch and scattered container distribution.

    Centralized Empty Container Yard

    The core demand of empty container yard is to improve the space utilization rate, and the high-level stacking capacity of trans-loader can greatly improve the storage capacity of empty containers per unit area, and at the same time, it can flexibly dispatch the empty containers to match the demand of different routes and different customers.

    Core Advantages of Container Transporter

    Strong operational flexibility

    Unlike rail lifting equipment, rubber tyred straddle carrier can move freely in the whole range of the yard, and the operation area is not restricted by the rail. When the layout of the yard is adjusted and the operation area is changed, there is no need to do any civil construction modification, and the equipment can directly switch the operation range, which is more capable of adapting to the business changes.

    Low preliminary infrastructure investment

    There is no need to pave the traveling track and pour the track foundation, and only need the yard floor to reach the conventional hardened bearing standard to be put into use. Small and medium-sized yards can significantly reduce the capital and time costs of the preliminary infrastructure, temporary transit yards such as short-term projects can also be quickly realized.

    Shorter Container Operation Process

    A single piece of equipment has both lifting and transferring functions, no need to repeatedly transfer containers between “yard bridge + truck”, reducing the waiting and alignment time of the intermediate links, and the cycle length of a single container’s on-site operation is shorter, which makes it less likely to be congested in the yard during peak hours.

    Higher storage density in the yard

    Relying on multi-layer stacking capacity, the vertical space of the yard can be fully utilized, and the storage capacity can be increased without expanding the site horizontally. In coastal port areas and urban logistics zones where land prices are high, the cost of site rental can be effectively diluted.

    Fewer ancillary equipment

    The traditional mode requires the simultaneous configuration of multiple types of equipment such as axles, tractors, and forklifts, while the trans-loader can cover all the operational aspects of the yard, reducing the types and number of equipment, as well as the complexity of equipment management and staffing.

    Controllable long-term operating costs

    Mature models have a high degree of commonality of wearing parts and transparent maintenance costs. Electric and hybrid models can further reduce energy consumption expenses, and from the perspective of the whole life cycle, the operating cost is lower than the traditional program of multiple equipment combination.

    Safe Operation

    Hyundai transporters are equipped with multi-level safety protection as standard, ranging from mechanical limit to electronic collision avoidance, and from load monitoring to emergency braking, covering the risk points of the whole process of operation. The standardized operation actions can also reduce the equipment collision and cargo damage problems caused by manual operation errors.

    Good scalability for future expansion

    Yard business increment, you can directly increase the purchase of equipment, do not have to synchronize with the large-scale infrastructure renovation, expansion flexibility is high, suitable for business in the upturn of the growth of the station.

    Comparison with other container handling equipment

    Many customers will take the cross-traffic truck and RTG, RMG, frontal crane, set of trucks to do the comparison, in fact, all kinds of equipment adapted to the scene is very different, there is no absolute advantages and disadvantages, only adapted to or not.

    Transporter vs RTG tire-type gantry crane

    RTG is mainly used for stacking operation in the fixed box area, horizontal transfer requires the cooperation of trucks; straddle carrier can independently complete the transfer + stacking, more flexible; RTG has a higher number of stacking layers, suitable for fixed large-capacity yards; straddle carrier is more suitable for the need for frequent transfers, the flow of fast yards.

    Straddle Car vs RMG Rail Mounted Gantry Crane

    RMG relies on fixed rail operation, strong stability, good automation adaptability, but high infrastructure costs, the layout is completely fixed; transporter low infrastructure costs, flexibility, automation transformation costs are relatively higher.

    Transporter vs Positive Crane

    Frontal crane is flexible in transferring, but the number of stacking layers is low and the operation efficiency is limited, which is suitable for small and medium volume and low operation frequency yard; straddle carrier has stronger stacking capacity and operation efficiency, which is suitable for medium and large volume of normalized operation yard.

    Straddle carrier vs Tractor trailer

    Tractor trailer is only responsible for horizontal transportation, no lifting capacity, must be used with lifting equipment; transporter is lifting + transportation integration, a single device to cover the whole process.

    Comparison Item Container Straddle Carrier RTG Crane RMG Crane Reach Stacker Terminal Tractor
    Mobility Full yard free movement Fixed block travel Fixed rail travel Flexible but low stack Only horizontal transport
    Core Function Lifting + transport + stacking Container stacking Container stacking Low stacking + short transfer Horizontal hauling
    Infrastructure Standard hardened yard Yard pavement + power supply Rail foundation + power Simple hardened ground Paved road only
    Initial Investment Medium Medium-high High Low-medium Low
    Maintenance Difficulty Medium Medium Medium-low Low Low
    Best Application Medium-large flexible yards Fixed container blocks High-volume fixed yards Small yards & depots Port internal transfer


    How to choose the appropriate container transporter?

    First accounting yard container throughput

    First of all, the average daily container handling volume, peak hourly operating volume, and then set aside 3-5 years of business growth space. In the hub yard with large throughput, the model with fast traveling speed and automated dispatching is preferred; in the small yard with smooth throughput, the standard configuration model can meet the demand.

    Adaptation with yard layout

    Check the width of the yard channel, turning space, box layout, and calculate whether the minimum turning radius of the equipment is suitable. Narrow aisles, box area dense yard, give priority to the selection of models with all-wheel steering, in-situ steering, to avoid poor vehicle traffic to lower the overall efficiency.

    Determine the rated lifting capacity

    Selection of tonnage according to the yard’s main container load, heavy boxes account for a high proportion of the selection of large tonnage, empty box-based selection of small tonnage. Do not blindly choose a large tonnage for the sake of “one-step”, and not to save money to choose the tonnage of the equipment is not enough, the risk of long-term overload operation is very high.

    Choose to match the power source

    The diesel model is suitable for all-weather, high-load operation, with low matching requirements; the hybrid model balances energy consumption and stability; the electric model is suitable for high environmental protection requirements, with charging support stations. It is necessary to combine the cost of local fuel and electricity, as well as the requirements of environmental protection policies to make a comprehensive judgment.

    Clear automation requirements

    If the yard has intelligent upgrading plan, you can choose the model with reserved automation interface, and then gradually upgrade the auxiliary alignment, remote control and unmanned function, without one-time full investment.

    Consider the site operating environment

    Coastal salt spray areas should choose marine grade anticorrosion coating, corrosion-resistant components; alpine areas should choose low-temperature start-up adapted power system; dusty areas should strengthen the sealing and dustproof design. Failure to adapt to the environment will significantly shorten the service life of the equipment.

    Confirmation of maintenance and spare parts supply

    Priority should be given to the models with strong commonality of parts and global spare parts supply from the manufacturers. Overseas projects, in particular, should confirm whether there is a local service network, can provide timely technical support, to avoid equipment failure after a long period of downtime waiting for spare parts.

    Calculate the total life cycle cost (TCO)

    Don’t just look at the purchase price of the equipment, but include energy consumption, maintenance, spare parts, downtime losses, and residual value. Often times energy-efficient models with a slightly higher purchase price have a lower total cost of ownership in the long run.

    Focus on the safety configuration

    Collision Avoidance System

    Laser or radar collision avoidance system can detect people, equipment and obstacles around the equipment in real time, and trigger early warning and automatic deceleration when the distance is too close to avoid collision accidents. It can also realize the anti-collision linkage between vehicles when multiple vehicles are operating in the same yard.

    Load monitoring system

    Real-time monitoring of spreader load, automatic alarm and restriction of lifting action when overloaded, avoiding damage to equipment structure and lifting parts from overloading operation, and preventing the risk of overturning caused by overweight box.

    Panoramic camera system

    Multiple cameras cover the blind area around the equipment, and the driver’s cab can view the spreader, tires, and box periphery in real time, eliminating the dead angle of the field of vision and improving the alignment accuracy and safety of the operation.

    Automatic braking system

    When encountering unexpected situations, releasing the operating pedal or power failure, the equipment can automatically trigger the brake to avoid skidding, falling loads and other dangers.

    Wind speed monitoring device

    Harbors and open yards are prone to windy weather. The wind speed monitoring system detects the ambient wind speed in real time and issues an early warning when it exceeds the safety threshold, reminding the operator to stop the operation or automatically locking the equipment to prevent rollover caused by high winds.

    Emergency Protection System

    Containing emergency power failure, emergency descent, emergency escape channel and other configurations, it can safely drop the load when encountering power failure or electrical failure, so as to protect the safety of operators and equipment.

    Equipment Maintenance Best Practices

    Daily spot check list

    Before every shift operation, we should do basic inspection, including tire air pressure, spreader locking pin, braking performance, hydraulic oil level, effectiveness of safety devices, to confirm that there is no abnormality before putting into operation, and eliminate minor faults before starting the machine.

    Preventive Maintenance Cycle

    According to the cycle of the equipment manual, change the oil, filter element, hydraulic fluid, wearable seals, tighten the structural bolts regularly, and do not wait for the parts to be completely damaged before repairing. The cost of preventive maintenance is much lower than emergency repairs, and can also reduce downtime losses.

    Hydraulic system maintenance

    Hydraulic transporter should focus on the hydraulic system, regularly check the oil cleanliness, pipeline sealing, timely replacement of filter elements and aging seals, to avoid hydraulic oil contamination caused by the valve group, cylinder damage.

    Regular inspection of tires

    Tires are the core bearing and walking parts, to regularly check the degree of wear and tear, air pressure, tread damage, abnormal wear and tear should be timely investigation of positioning, steering parameters. Yards with poor site conditions should appropriately increase the frequency of inspection.

    Electrical system maintenance

    Regularly clean up the electrical cabinet dust, check the tightness of the terminals, moisture and corrosion prevention. Electric models should focus on the maintenance of battery packs, charging and discharging according to specifications to extend battery life.

    IoT predictive maintenance

    Middle and high-end models can be equipped with IoT predictive maintenance system, real-time monitoring of motor, hydraulic, transmission components of the operating data, in advance of the risk of failure, and take the initiative to arrange maintenance, to minimize unplanned downtime.

    Industry Development Trends

    Electrification

    As the global green port policy continues to advance, the market share of electric container trucks is increasing year by year, and the battery technology is constantly being iterated, with range and fast-charging capability continuously enhanced, which will gradually become the mainstream model in the future.

    AI Fleet Management

    In a multi-vehicle cooperative operation yard, using AI algorithms to do fleet scheduling and path optimization can reduce idling, improve operational efficiency, and significantly improve the flow efficiency compared with manual scheduling.

    Remote Control

    Operators can remotely control multiple units in the center control room, eliminating the need to go to the driver’s cab on site, which improves the working environment and reduces the cost of manpower allocation at the same time.

    Automatic Driving

    Fully driverless trans-shipment trucks have been applied in several automated ports, and will be gradually popularized to medium-sized yards with the maturity of navigation and scheduling technologies.

    Digital Twin

    Digital twin technology is used to build a virtual model of the yard and equipment, simulate the operation process, predict equipment failures, and realize digital management of yard operation and equipment maintenance.

    Green Port Support

    Under the goal of carbon neutrality in ports, the emission reduction and energy saving technologies of trans-shipment vehicles will continue to be upgraded, and various technology routes such as hybrid, electric, and hydrogen fuels will be implemented in parallel to meet the environmental protection requirements of different regions.

    Frequently Asked Questions

    What is the rated lifting capacity of a container truck?

    The rated capacity of mainstream standard models focuses on 35-50 tons, covering the operation needs from regular empty containers to fully loaded containers, while special heavy-duty scenarios can be customized for large tonnage models up to 60 tons.

    How many layers of containers can a straddle carrier stack?

    Conventional models can stack 2-4 layers, that is, 1-over-2 to 1-over-4 configurations, high-level stacking models can be up to 5 layers, the specific combination of lifting height and yard safety requirements to choose.

    Which industries will use container trucks?

    It is mainly used in container ports, railroad intermodal terminals, inland container yards, logistics distribution parks, empty container distribution centers, and all the scenarios that require container stacking and transferring can be used.

    What is the core difference between straddle carrier and RTG crane?

    RTG is a tire-type gantry crane, mainly in the fixed box area to do stacking operations, horizontal transfer needs to be set with the truck; transporter is self-propelled equipment, lifting, transfer, stacking in one, more flexible, the operation covers a wider range.

    How much does a container transporter cost?

    The price is greatly affected by the tonnage, configuration, power type, and automation degree, ranging from several hundred thousand to millions of dollars, depending on the parameter configuration, customization needs to account for the exact quote.

    How long is the service life of a transporter?

    Under the premise of normal maintenance and compliant operation, the service life of diesel model is 15-20 years, the battery pack of electric model can be replaced, the service life of the main structure is comparable to that of diesel model, and the reasonable maintenance can reach a long service cycle.

    Is it worth to invest in electric transporter?

    For the annual operating hours sufficient, high environmental requirements, electricity price has the advantage of the station, electric models of long-term energy consumption and maintenance costs are lower, the whole life cycle of the revenue is very substantial, is worth considering the direction of the selection.

    What kind of maintenance is required for transporters?

    It mainly includes daily inspection per shift, regular fluid and wear parts replacement, hydraulic system inspection, tire maintenance, dust removal and fastening of the electrical system, as well as regular structural inspection and calibration of safety devices.

    Conclusion

    Choosing the right container straddle carrier is never about choosing the model with the highest parameters and the most expensive price, but about matching completely with the yard’s throughput, layout, business model, and long-term planning.

    From parameter selection to power configuration, from safety protection to maintenance system, each item affects the operational efficiency, life cycle and operating costs of the equipment. Combined with their own scenarios to do targeted selection, reserve a moderate upgrade space, in order to allow the equipment in the full service cycle to create a stable value, but also to better match the future pace of development of container logistics.

    Contact us

    Reliable Container Straddle Carrier Manufacturer

    Henan Mine Crane Industrial Straddle Crane Industrial has many years of experience in the development and manufacture of port logistics lifting equipment, and can provide customized container straddle carrier solutions for global customers.

    Our equipment has passed CE, ISO and other international certifications, with mature structural design, diesel, hybrid and electric power system options, with automation upgrade program, suitable for seaports, rail yards, inland logistics parks and other scenarios.

    From the preliminary program design, manufacturing, to on-site installation and commissioning, operator training, to the global supply of spare parts, 7 × 24 hours after-sales technical support, we provide a full range of supporting services to help customers choose the right container handling solutions to meet their needs.

    Contact our lifting technology team for a customized container yard handling solution.

    Henan Mine CraneDiscuss your requirements ↗
  • Container Handling Gantry Cranes: Spreader Bar Selection and PLC Alignment Control

    Container Handling Gantry Cranes: Spreader Bar Selection and PLC Alignment Control

    Container Handling Gantry Cranes: Spreader Bar Selection and PLC Alignment Control

    In ports and intermodal terminals, the operating accuracy of container gantry cranes directly determines the operating efficiency of the terminal.Most of the problems of shaking, alignment deviation, and frequent failures are due to improper selection of 20ft and 40ft container spreaders and mismatch with the integration of PLC alignment control system.

    This article combines the different application scenarios of RTG and RMG gantry cranes to systematically explain the selection specifications of spreaders, the principle of PLC precise alignment control, the logic of hardware and software integration, common matching faults, and scenario-based configuration plans, so as to provide a professional and landing technical basis for port equipment procurement, operation and maintenance upgrades and automation transformation.

    What Is a Container Handling Gantry Crane?

    Container gantry cranes are large-scale industrial lifting equipment designed for container loading, unloading, transshipment, and stacking operations. They are the core infrastructure for modern operations in ports, logistics hubs, and inland depots, and support the circulation and transportation of millions of standard containers (TEU) around the world every year.

    For container operation scenarios, the operating efficiency, safety and stability of gantry cranes depend entirely on the configuration of the equipment structure, the adaptability of the spreader and the coordinated matching of the control system.In-depth understanding of its structural principles, equipment differences and control logic is the core prerequisite for enterprise selection, equipment transformation, and site efficiency improvement.

    Core structure

    Container gantry crane is a complete set of equipment with highly integrated mechanical structure and electrical control system. The major subsystems work together to achieve safe, efficient and stable container operations. The core components are as follows:

    • Gantry structure: As the core load-bearing steel structure of the equipment, it is formed by splicing the outriggers on both sides with the main beam on the top, carrying all the loads of all crane mechanisms, spreaders and containers, and transmitting the force to the walking foundation.The span, lifting height, and cantilever length of the gantry are all customized according to the site layout, container stacking height, and operating range, which are the basis for the stable operation of the equipment.
    • Lifting mechanism: responsible for the lifting of spreaders and containers, the core includes lifting motors, reels, wire ropes, pulley blocks and other components.The lifting speed, working level, and wire rope configuration need to match the rated load of the equipment and the number of operating cycles per hour, which directly determines the operating efficiency of the site.
    • Trolley operating mechanism: equipped with a lifting mechanism and a spreader, it walks laterally along the main beam to achieve precise horizontal alignment of containers within the span of the crane. It is the key mechanical structure for precise stacking and alignment.
    • Cart operating mechanism: drive the entire crane to walk along the yard track or on the ground to realize the displacement of equipment across container columns and work areas, greatly expand the coverage of equipment operations, and adapt to the needs of large-area yard operations.
    • Container spreader: The core operating accessories that are directly docked with the container, and the corners of the container are bitten by the rotary locking mechanism to complete the container grabbing and release.The type, parameters, and functional configuration of the spreader directly determine the container specifications and operating modes to which the equipment is adapted, which is the core focus of the selection.
    • Electrical control system: it covers the power supply system, frequency conversion drive system, and PLC core control system, which is the “brain” of the entire equipment.Modern container gantry cranes rely on PLC to realize collaborative control of all actions, and can realize full-level automation operations from manual operation, semi-automatic circulation to fully automatic precise alignment.

    Container gantry crane application scenarios

    With the advantages of strong adaptability, large load and high degree of automation, container gantry cranes are widely used in all scenarios of multimodal transport. The core deployment areas include:

    • Container terminal: As the core operating hub of the seaport, it mainly undertakes the loading, unloading, storage and transit of containers between ships, depots, warehouses, and railways. It is the core node of the flow of foreign trade shipping containers.
    • Multimodal transport yard: it connects the core transit stations of the three major transportation systems of sea, railway and highway, and opens up the barriers to the connection of different modes of transportation to achieve efficient container turnover, rapid distribution and seamless circulation.
    • Port and logistics center: A comprehensive logistics distribution hub, which can be adapted to the warehousing, turnover, sorting, and stacking operations of ordinary bulk cargo and standard containers at the same time, and can be adapted to diversified logistics and freight scenarios.
    • Railway freight yard station: It focuses on the automated loading, unloading, storage and on-site reverse transportation of railway containers. It is the core supporting equipment scene for railway container trunk transportation and public railway intermodal transportation.
    • Shipyard: It is mainly used for precise hoisting, shifting and transshipment of ship modular container components, marine supporting equipment and materials, and is suitable for the construction needs of heavy materials in shipbuilding projects.
    • Industrial manufacturing and warehousing base: adapt to the needs of industrial-scale freight, and be responsible for the reception, transshipment and storage of containerized raw materials, semi-finished products, and finished products to ensure the efficient operation of the industrial supply chain.

    It is worth noting that the operating environment (indoor/outdoor, open-air/closed site, wind conditions, stacking height) will directly determine the selection of spreaders and the configuration of the control system, which is the core basis for equipment customization.

    RTG, RMG vs ordinary gantry crane

    According to the walking mode, structural characteristics and applicable scenarios, container gantry cranes are mainly divided into three categories: tire type (RTG), rail type (RMG) and fixed yard gantry cranes. The operating environment of different equipment directly determines the selection criteria for spreaders and control systems.

    Tire-type container gantry crane (RTG)

    It uses rubber tires to walk without laying special tracks, and the site is extremely adaptable, and the working area can be flexibly switched and the layout of the yard can be adjusted.The equipment mostly uses diesel power generation for power supply, which is not limited by external power supply, and is suitable for open-air container depots and dynamic turnover scenarios.RTG comes standard with telescopic spreaders, which are suitable for multi-specification container operations. The core advantages are strong mobility and flexible deployment, which are suitable for small and medium-sized terminals and logistics depots.

    Rail container gantry crane (RMG)

    Rail container gantry cran Walking along a fixed track, it has strong structural rigidity, high operating stability, excellent positioning accuracy, and higher rated load and operating cycle efficiency.The equipment is driven by full electric power and is suitable for automated, high-throughput standardized container terminals. It is widely used in large ports, railway hubs, and automated depots. It can achieve millimeter-level precision stacking and adapt to high-density and high-frequency operations.

    Fixed yard gantry crane

    The operation span and area are fixed, there is no wide-range walking capacity, the structure is simple, the cost is lower, and the maintenance is convenient. It is only suitable for lightweight operation scenarios with a single operation area and fixed-specification containers, and it is mostly used for industrial warehousing and small special depots.

    Impact of the environment on the configuration of the equipment

    RTG for open-air operations needs to be adapted to wind, uneven ground, container placement deviation and other issues, and must be equipped with telescopic spreaders and anti-swing PLC control systems; orbital RMG automation stations have extremely high positioning accuracy requirements and need to be equipped with encoders and LASER sensing high-precision PLC alignment systems; indoor fixed operating equipment is stable in working conditions, and only fixed spreaders and basic control logic can be configured to meet the needs.

    Container Spreader Bar Selection: What Should You Consider?

    The spreader is the only docking carrier between the crane and the container. Whether the selection is reasonable directly determines the safety of the operation, the efficiency of the operation and the service life of the equipment.Mismatched spreaders can lead to problems such as alignment deviation, locking failure, and excessive load, causing safety hazards and loss of production capacity.

    Adapt to container specifications

    The mainstream specifications of international standard containers are divided into 20 feet, 40 feet, and 45 feet. The spreader needs to be accurately adapted to the position of the corner parts of the container in order to achieve stable locking and hoisting. It is also the core selection basis for 20-foot container spreaders and 40-foot container spreaders.

    • 20-foot container spreader: it is divided into two types: fixed and telescopic. It is specially designed for 20-foot standard containers. It is suitable for special depots that only operate small boxes. It can also be used with a double crane mode to increase the amount of work.The structure is light, the response is fast, and the maintenance is simple.
    • 40-foot container spreader: The most widely used standard spreader on the market, with a rated load of up to 35-50 tons, suitable for most ordinary container operation scenarios, and extremely versatile.
    • 45-foot container spreader: customized for high-box and wide-body 45-foot containers, it is mostly used in European foreign trade logistics and special container transit stations, and is a special accessory for scene-oriented.
    • -elescopic spreader: the length of the frame can be adjusted independently, compatible with 20/40/45-foot multi-specification containers, suitable for mixed-loading operation depots, flexible and full, and is the first choice for comprehensive logistics hubs.
    • Fixed spreader: it is only suitable for single-specification containers. It has a simple structure, light weight, low failure rate and lower cost. It is suitable for special stations with fixed working conditions and single-box operations. The disadvantage is that it has no versatility and cannot be adapted to multi-specification container mixed operations.

    Single crane vs double crane spreader

    Single box spreader: The industry’s general standard configuration, only 1 container can be hoisted at a time, suitable for most conventional operating scenarios, the equipment load pressure is low, the operation is stable, and the operating threshold is low.

    Double-box spreader: dedicated and efficient configuration, which can lift two 20-foot standard containers at the same time. The core advantage is to greatly increase the throughput of operations. In ports and transit stations dominated by 20-foot small containers, the operating efficiency can be almost doubled and the number of crane operation cycles can be reduced.

    However, the mechanical structure of the double crane system is more complex, and the load, structural strength, and control synchronization of the crane are more demanding.For 40/45-foot large box-based, low-throughput industrial depots, the operation and maintenance costs and equipment losses of the dual-crane configuration will be greater than the efficiency gains, and there is no need to choose blindly.

    Load rating and safety design

    The selection of the rated load of the spreader and crane cannot only refer to the nominal size of the container. The comprehensive total weight needs to be calculated, including the weight of the container, the weight of the cargo in the box, the weight of the spreader and the weight of all hoisting accessories.

    The maximum total weight of a standard 40-foot container can reach 30,480 kg. After superimposing the weight of the spreader, accessories and the eccentric load of the cargo, the actual operating load is much higher than the nominal value.Sufficient safety margin must be reserved for the selection of models, and industry standards such as ISO 1161, ISO 3874, FEM, and ASME must be strictly followed.

    If the load selection is too small, it will cause major safety accidents such as equipment deformation, hoisting failure, and falling boxes; if the load selection is too large, it will cause a waste of equipment resources and reduce the efficiency of the operation cycle. It is necessary to accurately match the selection of working conditions.

    Rotary lock structure and control logic

    The rotary lock is the core connecting component of the spreader and the container, and its locking feedback and control interlocking are the core guarantee of hoisting safety.

    Fully automatic rotary lock: driven by hydraulic pressure or motor, the lock and unlock are uniformly controlled by PLC without manual intervention. It is a standard configuration of modern automated cranes with efficient operation and low error rate.

    Manual rotary lock: relying on manual on-site manual completion of locking and unlocking operations, the process is cumbersome, the operating efficiency is low, and it is easily affected by human operating factors, and there are operating deviations and safety risks.It is only suitable for lightweight job scenarios with low job frequency, simple working conditions, and low automation requirements.

    The equipment is equipped with a special position sensor, which can feedback the locking/unlocking status of the rotary lock in real time, and form a hard interlock with the PLC control system: the fully locked state is not detected, and the system prohibits lifting; the container is not fully landed, the load is not unloaded, and unlocking is prohibited, and dangerous operations such as unlocking and lifting the hanging box are eliminated from the root cause.

    How PLC Alignment Control Improves Container Positioning

    Gantry crane PLC control system and container alignment system are the core of modern crane automation operations. All actions are coordinated through programmable logic controllers to solve industry pain points such as container alignment deviation, shaking, and inaccurate positioning.

    What is PLC alignment control

    PLC (Programmable logic controller) is an industrial-specific core control unit that can collect sensor signals in real time, execute preset control logic, output precise action instructions, and coordinate the whole process of crane operations.In the container gantry crane, the PLC core coordinates and controls the following modules:

    • Lifting system: it can carry out precise and closed-loop global control of lifting height, operating speed, acceleration and deceleration curves, dynamically optimize the operating attitude of load lifting, completely avoid lifting jitter, speed mutation and other problems, and ensure stable, accurate and controllable lifting operations throughout the process.
    • Trolley walking: equipped with a high-precision horizontal alignment control system, with a flexible start-stop intelligent strategy, it effectively eliminates the start-stop impact and alignment deviation, greatly improves the horizontal alignment accuracy, guarantees the alignment fit of the box, and stably adapts to refined stacking operations.
    • Cart walking: it has the ability of long-distance walking and dynamic positioning and calibration of the yard, which can effectively offset the cumulative positioning errors caused by long-distance operation, and ensure that the positioning accuracy of the equipment is consistent within the global operating range, the walking operation is stable, and it is suitable for large-area yard operation scenarios.
    • Spreader adjustment: accurately control the telescopic stroke and alignment error of the telescopic spreader, and can be adaptively adapted to multi-specification container loading and unloading operations, with high adjustment accuracy and strong adaptability to meet the needs of diverse yard operations.
    • Rotary lock mechanism: it can accurately output standardized locking and unlocking control instructions, and simultaneously collect data on the operating conditions and operating status of the mechanism in real time to realize the status monitoring and feedback of the whole process to ensure accurate response, safety and reliability of the rotary lock action.
    • Safety interlocking: all-weather global monitoring of equipment operating parameters and operating conditions, relying on a mature intelligent logic interlocking protection mechanism, actively intercept illegal operations, avoid operational risks, and build a strong safety line of defense for container hoisting operations from the equipment control level.

    Through millisecond-level data operation and command output, the PLC cooperates with the frequency conversion drive system to realize the smooth operation, precise alignment, anti-shake and shock absorption of the crane, and completely solves the accuracy shortcoming of manual operation.

    The difficulty of precise alignment

    Container automated stacking and alignment operation scenarios are complex, there are many external interference factors, and the equipment control accuracy and operating stability requirements are extremely high. It is the core difficulty of the automation control of the whole machine. The main operational interference factors on the site are as follows:

    • Outdoor environmental interference: The equipment is operated in an open open-air yard without a closed protective structure. Natural wind and gusts of wind can easily disturb the floating containers, causing the box to shake and shift its position, which directly reduces the alignment accuracy and affects the stacking quality.
    • Load shaking interference: During the start-stop and variable-speed walking of the equipment, the wire rope is prone to pendulum swing, which drives the hoisting container to continue to shake and shift, and cannot quickly complete the precise alignment and stable drop-off, which seriously affects the operating efficiency and stacking accuracy.
    • Limitations of artificial field of vision: In long-distance, high-level stacking operation scenarios, the field of vision of manual operation is limited, the alignment accuracy is insufficient, the operating efficiency is low, and the fault tolerance rate is low.
    • Long-distance positioning error: The yard operation has a large span and a long walking distance, and the operation of the equipment is prone to cumulative errors, which eventually leads to the offset of the container alignment.
    • High-precision stacking requirements: Multi-layer container stacking operations have strict accuracy requirements, and they need to meet the millimeter-level standard. Small alignment deviations can cause safety hazards such as offset of the whole stack and collision of the box.
    • Container placement deviation: The placement of containers at the bottom of the yard is prone to irregularities and misalignment, which puts forward extremely high requirements for real-time adaptive calibration and accurate alignment of equipment.

    Core sensor configuration

    The whole machine relies on a PLC closed-loop intelligent control system and is equipped with a full set of high-precision sensing equipment to collect core operating condition data such as equipment displacement, speed, attitude, and status in real time, and provide real-time feedback and dynamic correction of operating parameters to provide core data support for automated and accurate operations. The sensor configuration and core functions are as follows:

    • Encoder: Collect the operating displacement and real-time speed of carts, trolleys, and lifting mechanisms with high precision in real time, build a full-dimensional position closed-loop control system, and correct the operating deviation in real time to ensure accurate positioning and controllable operation during the whole process of equipment walking and lifting.
    • Proximity sensor: intelligent detection of the presence or absence of the container and the state of the spreader in place, accurate triggering of linkage actions such as dropping the box, rotating the lock and locking, to ensure the smooth connection of the operation process.
    • Position sensor: real-time dynamic feedback on the extension length of the telescopic spreader, accurately adapt to different specifications of container operations, and ensure the adjustment accuracy of the spreader.
    • Anti-sway sensor: collect load sway data in real time, and cooperate with PLC intelligent algorithms to correct the operating actions of the equipment, effectively suppress the sway of the box, and improve operation stability and alignment efficiency.
    • Load cell: real-time monitoring of container load weight, overload protection, load balance detection and accurate determination of drop-off status, to avoid the risk of overload operations.
    • Rotary lock position sensor: feedback the locking and unlocking working status of each group of rotary locks around the clock, monitor the locking reliability in real time, and ensure the safety of hoisting operations from the source

    PLC Alignment Control Workflow: From Detection to Placement

    Relying on standardized PLC closed-loop control logic, the system runs through the entire operation link of container grabbing, transshipment, alignment, and drop-off to achieve automation, high-precision, and high-safety control of the whole process. The entire operation process is divided into six closed-loop controllable steps.:

    Step 1: target position detection

    PLC integrates encoder position data, laser ranging sensor signals and yard management system coordinate information to accurately calibrate the container capture point and the target drop-off point to build an accurate and reliable operation coordinate reference to provide data support for subsequent automated operations.

    Step 2: the crane moves in concert

    The system adopts a multi-axis collaborative linkage control strategy, and the PLC synchronously dispatches the long-distance walking of the trolley yard, the precise horizontal alignment of the trolley, and the height adjustment of the lifting mechanism. The multi-mechanism synchronously cooperates and cooperates accurately to quickly complete the equipment in place, effectively shortening the operating cycle and improving the overall operating efficiency.

    Step 3: Load ablation calibration

    When the equipment approaches the target position of the operation, the PLC automatically activates the intelligent anti-swing algorithm, dynamically optimizes the acceleration and deceleration operation curve of the equipment, and actively suppresses the swing, offset and jitter of the container during the hoisting process, so as to achieve stable and controllable load attitude, and lay a solid foundation for high-precision alignment and smooth box drop.

    Step 4: precise alignment of the spreader and the container

    Step 5: Rotary lock lock confirmation

    After the spreader is accurately positioned to fit the container, the PLC outputs a precise locking control command, which drives the rotary locking mechanism to complete the reliable bite locking.After the system receives all the feedback signals that the rotary locks are in place and locked, the lifting operation authority can be unlocked, and major safety hazards such as virtual locks and missed locks can be eliminated from the control level.

    Step 6: Unlock the safe drop box

    Throughout the drop-off operation, the load cell dynamically collects load data in real time and determines the force state.Only after confirming that the container is fully landed and the load is completely detached from the spreader load, the system will perform the unlocking action, effectively avoiding the risks of violations such as unlocking the hanging box and unlocking the load, and ensuring the safety and standardization of the entire operation.

    Spreader and PLC Integration: Why the Two Systems Must Be Designed Together

    The spreader is not a simple mechanical accessory, but the core terminal execution unit of the PLC control system.The deep integration, data exchange, and logical linkage of the two are the core of the safe, efficient, and stable operation of the crane, as well as the top priority of equipment design and transformation.

    Data communication mechanism between spreader and PLC

    During the whole operation, the spreader and the PLC system maintain high-speed two-way data exchange, synchronize the operating status of the equipment and operating conditions in real time, and build a closed-loop linkage control system. The core interaction content is as follows:

    • Rotary lock status feedback: real-time collection and upload of rotary lock locking, unlocking and abnormal fault status signals, to provide the core data basis for the safety interlocking logic control of the whole machine and the operation safety determination, to ensure that the locking action can be monitored and traceable throughout the process.
    • Telescopic feedback of the spreader: dynamically and synchronously feedback the actual stroke and in-place status of the telescopic spreader, accurately match the operating requirements of containers of different sizes, and realize rapid switching and precise adaptation of multi-specification boxes.
    • Issuance of control instructions: relying on the PLC core control system, it accurately outputs various action instructions such as rotary lock locking, unlocking, and spreader expansion and adjustment. The instructions respond quickly and are executed accurately, and the whole process of equipment automation is stably realized.
    • Fault early warning reporting: monitor the operating status of core components such as sensors and actuators around the clock, capture abnormal working conditions in real time, and trigger alarms and safety protection mechanisms in time to avoid equipment failures and hidden dangers in operations in advance, and ensure the stable operation of the equipment.
    • Global sensor data synchronization: high-speed synchronous transmission of multi-dimensional sensor data such as position, load, and laser ranging, providing real-time and reliable data support for core operating functions such as precise alignment of equipment, stable load control, and flexible start and stop.

    PLC input and output (I/O) core control logic

    This container crane is equipped with a mature PLC intelligent control system and a standardized I/O signal configuration, which can realize the full-link closed-loop precise control of equipment operations and ensure the stable, safe and efficient operation of automated operations.

    Input signal (acquisition feedback): real-time collection of container in-place status, rotary lock locking/unlocking working conditions, spreader telescopic position, spreader fault alarm, real-time load value, equipment alignment deviation and other core signals, capture equipment operating conditions in all directions, and provide accurate data support for intelligent system control.

    Output signal (execution command): accurately output control instructions such as rotary lock lock/unlock control, equipment sound and light early warning, stepless speed regulation of cart/trolley/lifting mechanism, lock/release of lifting authority, etc., to achieve accurate response and coordinated linkage of the actions of each mechanism.

    All operating data, status signals and fault information of the system can be visualized in real time through the HMI man-machine interface, which is convenient for operators to intuitively grasp the operating conditions of the whole machine, realize the seamless switching between fully automatic operations and manual intervention, and improve the flexibility and controllability of operations.

    Core security interlocking logic

    The PLC system has built-in multiple closed-loop safety interlock protection logic, which builds a safety protection barrier from the bottom of the program to avoid the risk of illegal operation and misoperation in all directions. The core interlock protection mechanism is as follows:

    • Locking safety interlock: Before the rotary lock completes the full stroke and is locked in place, the system forcibly locks the lifting action authority, prohibits the execution of hoisting and transshipment operations, and eliminates the safety hazards of unpacking and dropping the box caused by the failure of the lock to bite from the root cause.
    • Floating protection interlock: When the container is detected to be in a state of floating force, the system blocks all unlocking instructions, prohibits the rotary lock from performing unlocking actions, and completely avoids high-risk risks such as high-altitude falling of the box and heavy-duty decoupling of equipment.
    • Precise alignment and speed limit interlocking: When the equipment enters the close-range precise alignment condition, it automatically switches to the low-speed stable control operation mode, which restricts the high-speed operation of the mechanism, effectively suppresses load shaking and position offset, and guarantees the accuracy of container stacking alignment and operation stability.
    • Abnormal fault interlocking: When the core sensor data is abnormal, the signal deviation exceeds the limit, or the equipment working conditions are abnormal, the system immediately triggers emergency shutdown protection, locks all mechanism actions, and aborts the operation process to ensure the safety of equipment, goods and on-site operations in all directions.

    HMI human-computer interaction and operation feedback

    The HMI human-computer interface is the core of the interaction between the operator and the equipment. It displays core data such as the telescopic status of the spreader, the alignment of the container, the working status of the rotary lock, the walking position of the crane, fault alarm information, and emergency stop status in real time. The interface is simple and intuitive, and it is suitable for high-load and high-intensity operation scenarios in the port, greatly reducing the difficulty of operation and the cost of troubleshooting.

    Anti-Sway and PLC Alignment: The Key to More Precise Container Handling

    Alignment control and anti-swing control cannot be operated independently. They must be deeply coordinated through the PLC system in order to achieve high-speed, accurate and stable stacking operations.A separate alignment control cannot solve the problem of load shaking, and a separate anti-swing function cannot guarantee the positioning accuracy.

    Through a unified algorithm, the PLC system cooperatively adjusts the lifting speed, trolley walking speed, trolley walking speed, and equipment acceleration and deceleration curve to suppress the container swing amplitude from the source: by predicting the load shaking law, the equipment action is corrected in advance to offset the offset caused by wind and start-stop inertia.

    The data of the actual station transformation case show that the RMG crane equipped with an integrated anti-swing PLC control system has increased its operating efficiency by 15%-20%, the container alignment accuracy is controlled within ±5mm, and the service life of vulnerable parts such as wire ropes and spreaders is extended by 25%, greatly reducing equipment operation and maintenance costs and downtime losses.

    At present, mainstream equipment adopts a hybrid scheme of ”mechanical shock absorption + electronic anti-shake”, the mechanical structure provides basic stability, and the PLC intelligent algorithm realizes precise fine-tuning, which is perfectly adapted to the complex port scenarios of open-air high winds and high-frequency operations.

    How to Select the Right Spreader and PLC Configuration

    Working condition evaluation parameters

    Before selecting the type, it is necessary to comprehensively sort out the operating parameters of the site and accurately match the configuration of the spreader and the control system: container specifications, maximum rated load, required lifting speed, hourly operating cycle volume, indoor/outdoor operations, site wind level, stacking height, positioning accuracy requirements, existing equipment control system architecture, automation level requirements.

    Scenario configuration reference scheme

    • Dedicated 40-foot container yard: suitable for single box type, stable working conditions, equipped with fixed 40-foot spreader, with basic PLC encoder alignment system and standard rotary lock safety interlock logic.The overall structure is simple and reliable, the operation and maintenance cost is low, and the stability is strong, taking into account the practicality of the operation and the cost performance of the project.
    • 20/40-foot mixed operation logistics yard station: adapted to the needs of alternating operations of multi-specification containers, telescopic adaptive spreaders are selected, and PLC control systems with real-time feedback of spreader length and high-precision laser alignment sensors can be used to quickly switch operating modes and adapt to diversified and flexible operating scenarios in the yard.
    • High-throughput port terminal: For high-frequency and high-throughput port operating conditions, it is equipped with dual-crane high-efficiency spreaders, with a high-end PLC integrated anti-swing control system, a multi-axis linkage precision positioning module and an HMI real-time working condition monitoring terminal, which greatly compresses the length of the operation cycle and improves the throughput capacity and operation stability of the yard in all directions.
    • Fully automatic unmanned yard: adapted to intelligent unmanned operation scenarios, equipped with electric telescopic high-precision spreaders, integrated multi-sensor fusion positioning system, remote monitoring PLC control system, can be seamlessly connected to the intelligent management system of the yard station, to achieve unmanned, automated and accurate operation of the whole process of container grabbing, alignment, and stacking.

    Common Problems When Spreader and PLC Systems Are Poorly Matched

    The mismatch between the spreader and the control system is the core cause of equipment failure, low efficiency, and frequent safety hazards in the station. The five common problems need to be avoided.:

    • Abnormal synchronization of the rotary lock signal: The electrical signal of the spreader does not match the parameters of the PLC module, and problems such as false locking and signal delay will occur. The system misjudges the hoisting state, resulting in dangerous lifting, which can easily cause safety accidents in falling boxes.
    • Insufficient positioning feedback accuracy: the sensor configuration is insufficient and the accuracy is not enough. The PLC cannot accurately judge the position of the spreader and the container. There are frequent alignment deviations and misalignment of the drop box, which require repeated manual correction, greatly reducing operating efficiency, and wearing out the container corners and equipment structure at the same time.
    • The control logic does not match the structure of the spreader: The fixed spreader is matched with the control logic of the telescopic spreader, or the telescopic spreader is adapted to a simple control program, which will cause chaotic instructions, frequent alarms, and equipment sudden stops, which will seriously affect the continuity of operations and increase the probability of equipment failure.
    • No anti-swing collaborative control: the PLC system, which only has the basic alignment function and does not integrate anti-swing logic, cannot suppress the shaking of the container, the operation waiting time is long, the alignment efficiency is low, and the risk of collision during high-speed operation is extremely high.
    • Excessive automation redundancy: blindly configuring a high-end fully automatic control system under simple and fixed working conditions will lead to complex equipment structure, increased failure points, significant increase in operation and maintenance difficulty and cost, and the problem of “excessive automation and extremely low cost performance”.
    • Core summary: The higher the automation configuration, the better. The spreader and PLC system must fit the actual operating conditions, site conditions and operation and maintenance capabilities, and adaptability takes priority over the level of intelligence.

    Safety and Reliability Considerations

    The PLC control system is only responsible for the optimization of the operation process and the coordination of actions. The core safety protection must rely on independent hardware loops to ensure the safety of equipment operation. The core safety configuration includes:

    • Overload protection: It is equipped with an independent weighing sensor overload circuit to monitor the load status in real time. Once the overload is detected, power failure and shutdown will be triggered immediately, and safety risks such as structural deformation and falling boxes caused by overload operations will be eliminated from the hardware level.
    • Emergency stop system: equipped with an independent hardware safety circuit, it is not disturbed by the operating state of the PLC program. In case of emergency, the power can be cut off with one key and the emergency shutdown can be stopped to ensure the safety of personnel and equipment.
    • Rotary lock hardware interlocking: Adopts a hardware-level locking protection mechanism, does not rely on software logic, and effectively avoids dangerous working conditions such as mislocking and false lifting caused by abnormal PLC programs and signal confusion.
    • Stroke limit protection: Multiple limit protections are set up within the full walking stroke of lifting, carts, and trolleys to prevent over-range operation, structural collisions, and mechanical damage, and to ensure the safety of equipment operation boundaries.
    • Anti-collision system: relying on high-precision ranging sensing to achieve regional protection, real-time monitoring of equipment spacing and surrounding environment, effectively avoid machine-to-machine, machine-to-yard structure collision accidents.
    • Wind monitoring system: The open-air model is equipped with a standard wind speed monitor, which collects on-site wind data in real time, and automatically restricts high-speed operation or shutdown under windy conditions to avoid the risk of load offset and equipment instability caused by strong winds.
    • Redundant safety feedback: For key safety parameters such as rotary lock status and overload signal, a dual-sensor redundant acquisition design is adopted to eliminate single-point failure blind spots and improve system operation reliability.
    • Electrical protection: Integrate a full set of electrical protection functions such as short circuit, overload, leakage, and insulation monitoring to stabilize electrical operating conditions and avoid downtime and safety accidents caused by electrical failures.
    • Preventive maintenance mechanism: through regular sensor calibration, control algorithm iteration, mechanical structure flaw detection and maintenance, the accuracy, stability and service life of the equipment are continuously guaranteed, and the probability of sudden failure is reduced.

    Conclusion

    The operating efficiency of container gantry cranes depends not only on the equipment body, but also on the collaborative integration of the spreader and the PLC control system.RTG is suitable for flexible yard operations, and RMG is more suitable for high-precision and high-throughput automated terminals. The selection should be combined with actual working conditions to match the spreader, sensor and control logic.

    Synchronous planning of spreader parameters, PLC control, anti-shake system and sensor configuration from the project design stage can improve operation accuracy and operating stability, and reduce failure and maintenance costs.Henan Mine Crane can provide RTG/RMG customized lifting solutions according to terminal layout, operation requirements and automation level to help the port achieve efficient and intelligent operation

    Henan Mine CraneDiscuss your requirements ↗
  • Complete Buying Guide for 50-Ton Heavy-Duty Gantry Cranes

    Complete Buying Guide for 50-Ton Heavy-Duty Gantry Cranes

    Complete Buying Guide for 50-Ton Heavy-Duty Gantry Cranes

    50-ton heavy-duty gantry cranes are widely used in heavy industry, ports, shipyards, warehousing and other heavy-duty scenarios. With the advantages of strong bearing capacity, stable operation, wide adaptability and high cost performance, they are the core equipment for industrial heavy-duty operations.As a large fixed asset, improper selection and mismatched parameters and configuration working conditions will directly reduce production efficiency, bury safety risks, and increase operation and maintenance costs.

    This article comprehensively combs the purchase points of 50-ton gantry cranes from the nine dimensions of equipment definition, model classification, core parameters, core accessories, price factors, manufacturer screening, safety configuration, operation and maintenance, and equipment comparison to help enterprises avoid procurement misunderstandings and accurately match highly adaptable and cost-effective equipment solutions.

    What Is a 50-Ton Gantry Crane?

    The 50-ton gantry crane is a high-strength and high-stability industrial heavy-duty lifting equipment, which belongs to the derivative category of bridge cranes.The equipment as a whole has a gated structure. The main beam spans the working area and is supported by floor-to-ceiling outriggers. There is no need to rely on the factory building. It can run independently on the ground track or tires. It is specially used for lifting, transshipment, and stacking of heavy goods with a rated load of 50 tons and below.

    The 50-ton rated load marked by the equipment represents the maximum load weight that can be safely hoisted under the premise of standard design conditions, compliance operation, and standard spreader, including the comprehensive weight of the cargo body, spreader, and accessories. Long-term overload operations are strictly prohibited.

    The complete set of equipment relies on the coordinated operation of the five core systems to achieve accurate and stable lifting operations:

    • Bridge structure: The core load-bearing body is divided into two mainstream structures, box-shaped and truss, including the main beam and the end beam. It mainly carries the full weight of the lifting trolley, the hoist mechanism and the cargo. It is the key to ensure the carrying capacity and structural stability of the equipment.
    • Support outriggers: Common A-shaped and box-shaped outriggers connect the bridge frame and the walking mechanism to evenly transmit the weight of the equipment and the weight of the load to the ground, resist shaking and external shocks during operation, and ensure the stability of the whole machine.
    • Lifting mechanism: it consists of a wire rope electric hoist, a lifting trolley, a motor, a reducer, a reel, a hook, and a braking system. It is responsible for the vertical lifting of goods and is the core execution unit to realize the lifting function.
    • Walking mechanism: it is divided into two types: orbital type and tire type. It consists of a walking wheel set, a drive motor, and a frequency conversion control system. It can realize the longitudinal movement of the whole machine along the working area and cover a wide range of working space.
    • Electrical control system: With PLC programmable controller as the core, it integrates the operation terminal, safety interlock, monitoring and early warning system, and co-ordinates the control of all actions such as lifting, walking, and trolley translation of the equipment to ensure accurate operation and safe operation.

    Main Types of 50-Ton Gantry Cranes

    According to the different structural forms, support methods, and walking configurations, 50-ton gantry cranes can be divided into four mainstream models, which are adapted to different sites, working conditions, and operating needs.:

    Full gantry crane

    Both sides are equipped with floor-to-ceiling outriggers, which run along the ground track throughout the process, and the whole machine is independently supported without relying on any building structure.It has a stable structure, strong carrying capacity and large operating range. It is suitable for outdoor large-scale heavy-duty hoisting scenarios and is widely used in shipyards, large steel depots, outdoor construction sites, and large storage bases.

    Semi-gantry crane

    The asymmetric structure of “single-sided outrigger landing + single-sided plant track beam support” is adopted, cleverly using the existing plant building, without the need to lay the track on the whole site, greatly saving installation space and infrastructure costs.It is suitable for indoor and outdoor connection operations in existing factories and workshops. It is the preferred model for the transformation of old factories and heavy-duty operations in limited space.

    Tire gantry crane (RTG

    Abandoning the traditional track structure, high-strength rubber tires are used as walking parts. There is no need to lay a fixed track, and they can be freely turned and flexibly shifted without being restricted by the track of the site.It is extremely mobile and suitable for scenarios such as container depots, logistics parks, temporary construction sites, etc. that require frequent switching of operating areas. The only shortcoming is that the equipment manufacturing cost is relatively higher.

    Double girder gantry crane

    It is the recommended standard model for 50-ton heavy-duty conditions.Compared with single-beam models, the double-beam structure has more uniform force and stronger structural rigidity. It has higher operating stability, greater lifting height and stronger load dispersion capacity. It can carry a rated load of 50 tons at high frequencies for a long time, and is perfectly adapted to high-strength and high-load heavy-duty operation scenarios such as steel mills, heavy industry workshops, and large prefabricated component factories.

    Key Specifications to Consider When Buying a 50-Ton Gantry Crane

    Rated lifting weight

    The rated lifting weight of 50 tons is the core parameter of the equipment. Two core points need to be clarified when purchasing: first, confirm whether 50 tons is a pure cargo load or the total load of ancillary accessories such as hoisting beams, grab buckets, electromagnetic suction cups, etc., to avoid insufficient actual available hoisting weight; second, take into account the current operating needs and future capacity expansion, and try to reserve a reasonable load margin.

    At the same time, it is strictly prohibited to select critical load equipment. If the equipment runs at full load and ultra-close to the rated load for a long time, it will accelerate the wear and tear of steel structures, braking systems, and motors, greatly shorten the service life of the equipment, reduce safety redundancy, and bury safety hazards such as equipment deformation and brake failure.

    Span 

    Span refers to the distance between the centers of the walking tracks on both sides of the equipment, which directly determines the operating coverage, structural design standards and procurement costs of the equipment, and is the key spatial parameter for selection.

    • Small-span model (10-20 meters): the structure design is simple, the weight is lighter, and the infrastructure and procurement costs are lower, but the operation coverage area is limited, which is suitable for fixed-point hoisting operations in small workshops and narrow areas.
    • Large-span models (more than 20 meters): can cover large-scale work areas and are suitable for large-scale yard, shipyard, and construction site operations, but the strength, bending resistance, and foundation bearing capacity of steel structures are required to be higher, and the cost of equipment and infrastructure are increased simultaneously.

    The selection of span needs to be strictly combined with the layout of the factory area, the size of the work site, the material handling route, and the planning of equipment placement. Under the premise of meeting the full coverage of the operation, the cost waste caused by excessive selection should be avoided.

    Lifting height

    The lifting height determines the maximum vertical height that the cargo can be lifted. The selection needs to integrate four scenario factors: the dimensions of the cargo itself, the height of the material stacking, the height of the production line equipment, and the clearance requirements of ground vehicles and equipment.

    Conventional 50-ton gantry cranes have a lifting height of 6-30 meters, and small and medium-height models can be selected in the indoor workshop to meet the needs of production assembly and equipment maintenance; outdoor depots, shipyards, and construction sites need to reserve sufficient height margin to adapt to cargo stacking, hoisting of large components, and vehicle traffic requirements to avoid insufficient height affecting the operation.

    Work level

    The working level represents the crane’s operating frequency, load cycle strength and durability level. It directly matches the strength of the working conditions and is divided into four levels: light, medium, heavy and overweight. It is the core parameter to avoid premature equipment aging and frequent failures.

    1. Light grade (A1-A3): low frequency of operations, length of daily work hours, intermittent operations, only suitable for equipment maintenance and sporadic hoisting scenarios.
    2. Intermediate (A4-A5): medium operating frequency, stable load, suitable for ordinary manufacturing workshops, conventional warehousing and transshipment operations.
    3. Heavy grade (A6-A7): high-frequency operations, frequent proximity to rated loads, suitable for high-intensity working conditions such as steel mills, shipyards, and prefabricated component factories.
    4. Super-heavy (A8): 24-hour continuous operation, full load cycle, suitable for large-scale assembly lines, port heavy-duty continuous operation scenarios.

    When purchasing, the work level needs to be accurately matched according to the daily operating time, the number of hoisting per hour, and the annual operating load. Low-level equipment used in high-intensity working conditions will be quickly damaged, and high-level equipment used in light-load working conditions will cause cost waste.

    Important Components of a Heavy-Duty 50-Ton Gantry Crane

    • The main body of the steel structure: As the core skeleton of the whole machine, it consists of the main beam, outriggers, and end beams, which directly determine the safety, service life, and operation and maintenance costs of the equipment.The high-quality models are made of high-strength steel, with standard welding technology, anti-fatigue structure and multi-layer anti-corrosion treatment. The key welds are tested by non-destructive flaw detection, which can effectively prevent rust, deformation and cracking, and greatly reduce the cost of late maintenance.
    • Lifting mechanism: The core operating unit consists of an electric hoist, a lifting trolley, a motor, a reducer, and a braking system, which are related to lifting efficiency and safety.The procurement focuses on matching the lifting speed required for working conditions, optimizing the brand’s core accessories, and confirming that the equipment is equipped with overload protection and dual braking system as standard, which can effectively avoid safety risks such as overload, slip hooks, and cargo falling.
    • Walking mechanism: it consists of walking track, wheel set, drive motor and VFD frequency conversion system, which is responsible for the longitudinal movement of the whole machine.Compared with traditional fixed-speed systems, VFD frequency conversion control can achieve smooth start-stop and stepless speed regulation, reduce mechanical impact and wear of accessories, improve cargo positioning accuracy, and adapt to high-precision, high-frequency and heavy-duty operations.
    • Electrical control system: with PLC controller as the core, it supports two operating modes: cab and wireless remote control.Integrated intelligent functions such as load monitoring, anti-swing, and remote fault diagnosis can avoid hoisting shaking, quickly investigate faults, and reduce downtime losses. Electrical accessories are waterproof, dustproof and anti-interference, and are suitable for all kinds of complex indoor and outdoor working conditions.

    How Much Does a 50-Ton Gantry Crane Cost?

    Overall price range

    The 50-ton gantry crane is a non-standard customized heavy-duty equipment. There is no fixed unified selling price. The market price span is very large. The core depends on the equipment configuration, working condition adaptation plan, and customization requirements.

    The price of rail-type 50-ton gantry cranes with standard conventional configuration is relatively affordable, while the price of large-span, high-lifting height, outdoor explosion-proof, intelligent automation, and tire-type models will be greatly increased. The cost of special RTG tire-type models for ports is much higher than that of ordinary industrial models.Therefore, quotations without complete parameters and working condition requirements do not have reference value.

    Core price influencing factors

    • Equipment design plan: double-beam models have stronger bearing capacity and higher configuration, and the price is higher than that of single-beam models; non-standard customized span, lifting height, cantilever structure, and special shape design will increase structural research and development and manufacturing costs, and increase equipment prices.
    • Material and manufacturing process: equipment using Q345B high-strength steel, high-standard non-destructive flaw detection welding, and thickened anticorrosive coating, the cost is much higher than that of ordinary steel and low-end equipment with simple welding technology; imported, first-line brand motors, brakes, and electrical accessories, the price is better than that of ordinary accessories, and the overall cost of equipment has increased synchronously.
    • Optional intelligent and safety functions: wireless remote control, intelligent anti-collision, outdoor wind and lightning protection, intelligent monitoring, explosion-proof system, remote diagnosis and other value-added configurations will increase equipment procurement costs, but can greatly improve the level of operation safety and automation.
    • Installation and transportation services: site foundation construction, track laying, transportation of the whole machine, on-site installation and commissioning, acceptance reporting, and localized after-sales supporting services for large-scale equipment will all be included in the overall procurement cost, and the service cost of off-site construction and complex site installation is higher.

    How to Select the Right 50-Ton Gantry Crane Manufacturer?

    Manufacturing experience

    Priority is given to manufacturers who have been deeply engaged in the lifting equipment industry for many years and have mature heavy crane production experience.Focus on verifying the landing project cases of manufacturers of heavy-duty gantry cranes of 50 tons and above, large-scale factory/shipyard/port cooperation experience, equipment export qualifications and overseas project experience.

    Mature manufacturers have perfect production processes and quality control systems, which can accurately match the needs of various complex working conditions, and avoid the problems of immature technology, rough workmanship, and unsecured after-sales service in small factories.

    Qualification and quality standards

    Regular manufacturers must have complete production qualifications and international certifications, core inspections: ISO quality management system certification, CE EU safety certification, national special equipment production license, and equipment must meet industry lifting equipment safety standards.Complete qualifications are the core guarantee of equipment quality, safety performance, and compliance, which can ensure that the equipment passes the local safety supervision and acceptance, and is put into use legally and in compliance.

    Evaluate customization capabilities

    The demand for 50-ton gantry cranes in different industries, sites, and working conditions varies greatly. High-quality manufacturers have perfect customized service capabilities.

    They can customize the span and lifting height according to the size of the customer’s site, and provide exclusive anti-corrosion, explosion-proof, and windproof protection solutions for special working conditions such as outdoor wind and rain, seaside salt spray, flammable and explosive, low temperature and high temperature. At the same time, it supports OEM customized services and adapts to various personalized procurement needs.

    After-sales service system

    Heavy-duty cranes are long-term industrial equipment, and perfect after-sales service is the key to ensuring the stable operation of the equipment.Before purchasing, it is necessary to confirm that the manufacturer can provide: full installation technical guidance, commissioning and acceptance of the whole machine, normalized maintenance services, rapid supply of original parts, 24-hour technical support and troubleshooting.Localized after-sales teams can significantly shorten the response time to failures, reduce equipment downtime losses, and extend equipment service life.

    Indoor vs Outdoor 50-Ton Gantry Crane Selection

    Indoor application scenarios

    Core advantage

    • Low corrosion and high stability: suitable for indoor closed operation scenarios, it can avoid external erosion such as wind, rain, ultraviolet rays, and sand, greatly reduce the loss of fuselage structure and electrical components, effectively reduce the probability of equipment failure, and ensure long-term stable operation.
    • Simple operation and maintenance, cost reduction and efficiency enhancement: the operating environment is clean and stable, and the daily maintenance and cleaning and maintenance process of equipment is simple, which greatly reduces manual operation and maintenance investment and effectively compresses later operation and maintenance costs.
    • Delay aging and extend life: Stable working conditions can reduce external interference, slow down the aging and loss of equipment components, significantly extend the service life of the whole machine, and improve the cost performance of the equipment.

    Suitable for industries: machinery manufacturing workshops, equipment assembly plants, hardware processing plant areas, indoor storage centers and other indoor heavy-duty operation scenarios.

    Outdoor application scenarios

    The outdoor open-air operating environment is complex and requires higher equipment protection performance. Special upgrades are required on the basis of standard models: the whole machine is thickened with anticorrosive coating, waterproof and dustproof electrical components, intelligent windproof braking system, lightning and rain protection devices, and some seaside and chemical scenes also need to be specially treated for salt spray and corrosion prevention.

    Suitable for industries: shipbuilding, steel yards, outdoor construction sites, port logistics, wind power engineering, large-scale prefabricated component factories and other outdoor operation scenarios.

    Maintenance Tips to Extend Gantry Crane Service Life

    Scientific daily inspection and regular maintenance can greatly extend the service life of the crane, reduce the probability of failure, and ensure operation safety. It is the core means to reduce the cost of the whole cycle of equipment.

    Daily pre-shift inspection

    Operators must complete a comprehensive basic inspection before daily operations. It is strictly prohibited for equipment to operate with diseases. The core inspection items are as follows:

    1. Wire rope: Regularly check the status of the wire rope, focusing on investigating defects such as broken wire, distortion, severe wear, etc., to ensure that the rope body is intact and the force is normal.
    2. Electrical and safety devices: Thoroughly inspect the electrical components such as operation buttons, indicator lights, sound and light alarms to ensure that the functions are intact and the operation is normal, and to ensure that the equipment safety interlock mechanism is effective.
    3. Hook assembly: Check the hook body for no cracking, deformation and other damage, confirm that the safety lock is sensitive to opening and closing, and the locking is reliable, and verify that the braking system has strong braking and no slippage failure problems.

    Regular special maintenance

    According to the frequency of equipment operation and the level of working conditions, hierarchical and regular maintenance work is carried out weekly, monthly, and quarterly. The specific contents are as follows:

    1. Regularly fill various moving parts such as wire ropes, bearings, gears, and walking wheels with lubricating grease to reduce component wear and ensure the smooth operation of the equipment.
    2. Check and tighten the structural bolts and track fixing bolts of the whole machine one by one to prevent safety hazards such as abnormal noise and offset caused by loose bolts.
    3. Normalize the oil level and oil status of the lubricating oil of the reducer, replenish the oil volume in time, replace the deteriorated oil stains, and ensure the stable operation of the transmission system.
    4. Comprehensively investigate the welds and paint surface conditions of the steel structure of the equipment, repair the rusted, cracked, and painted parts in a timely manner, and protect the structural integrity of the equipment.

    Professional annual inspection

    Every year, third-party professional institutions are invited to carry out safety testing and load testing to verify the rated load performance of the equipment, the sensitivity of the safety device, and the structural stability; establish a replacement ledger for wearing parts, and plan the replacement in advance according to the service life of the parts to avoid sudden failures caused by the aging of the parts.When the equipment is idle, it is necessary to lock the windproof device, cut off the power supply, and protect the whole machine.

    50-Ton Gantry Crane vs Other Heavy Lifting Equipment

    50-Ton Gantry Crane vs Overhead Crane

    Contrast dimension 50 ton gantry crane Overhead Crane
    Installation method Ground track/tire support, independent floor installation Relying on the track beam at the top of the plant, the building structure needs to be supported
    Scene flexibility The outdoor adaptability is extremely strong, it can be flexibly shifted, and it can be adapted to open-air venues. Only suitable for indoor fixed factories, with large scene limitations
    Infrastructure transformation No need to retrofit the factory building, low infrastructure cost and short construction cycle The structure of the plant needs to be strengthened and the top track needs to be erected, and the cost of transformation is high.
    Core application scenarios Outdoor depots, construction sites, shipyards, and open-air operations without factories Indoor fixed workshop, normalized indoor assembly and hoisting

    50-Ton Gantry Crane vs Mobile Crane

    • Cost of use: gantry cranes are put into operation at one time and reused for a long time, and the cost of a single crane for repeated operations on a fixed site is extremely low; car cranes need to continue to pay for fuel, leasing, and labor costs, and the cost of long-term high-frequency operations is higher.
    • Operating stability: The gantry crane has a fixed rigid track, stable structure, low shaking, and high safety; the car crane relies on outrigger support, which is greatly affected by the ground terrain, and the stability of heavy-duty operations is weak.
    • Long-term production capacity: Gantry cranes are designed for high-frequency cyclic operations on fixed sites, which can operate continuously all year round and have stable production capacity; automobile cranes are suitable for temporary, short-distance, and multi-site scattered hoisting, and the efficiency of long-term fixed operations is much lower than that of gantry cranes.

    Conclusion

    The procurement of 50-ton gantry cranes needs to be based on the comprehensive consideration of working condition adaptation, equipment reliability and long-term use value. Don’t just value the price. It should be selected in combination with equipment parameters, operating environment and future expansion needs to ensure that the equipment is adapted to production scenarios.

    High-quality 50-ton gantry cranes need to have a stable structure, reliable accessories and complete safety protection. Relying on customized design and strict quality control by professional manufacturers, they can effectively reduce failure and operation and maintenance costs, and ensure the safe and efficient long-term operation of equipment.

    Henan Mine Crane focuses on all kinds of heavy-duty lifting equipment and intelligent solutions. Relying on mature engineering experience, strict manufacturing standards and customization capabilities, it can provide customers with a one-stop full set of services from program design, manufacturing to floor-to-ceiling installation.

    Henan Mine CraneDiscuss your requirements ↗
  • Common Gantry Crane Accidents and How to Prevent Them

    Common Gantry Crane Accidents and How to Prevent Them

    Common Gantry Crane Accidents and How to Prevent Them

    Gantry cranes are widely used in industrial scenarios such as port loading and unloading, construction site construction, and material transfer in factories. They are the core lifting equipment for heavy material handling and hoisting of large components.In long-term outdoor complex working conditions and high-frequency operating environments, gantry crane equipment failures, illegal operations by personnel, harsh environmental interference and safety management loopholes can easily cause common safety accidents such as gantry crane falling objects, equipment collisions, and overturning of the whole machine, which directly cause equipment damage, project downtime, economic losses and casualties.Most industrial gantry crane safety accidents are caused by the accumulation of daily hidden dangers and insufficient safety protection. A good job in the analysis of the causes of gantry crane accidents and the normalization of safety prevention and control are the key to ensuring the stable operation of lifting equipment and avoiding the risks of hoisting operations.

    Overloading and Dropped Load Accidents

    Exceeding rated capacity

    Henan Mine Crane manufactured gantry crane overload operation and load fall are the most common safety accidents, and they are also the main causes of deformation and fracture of the lifting structure and casualties on the site.The rated lifting weight of each industrial gantry crane manufactured by Henan Mine Crane is strictly designed according to the carrying limit of core accessories such as the main beam structure, wire rope, hoist, etc., which is a hard standard for its safe and stable operation.In order to catch up with the construction period, many construction sites are overloaded with luck and violations. The weight of the material is estimated only empirically, ignoring the superimposed effects of wind loads and dynamic impact loads. Long-term overloaded operation will cause deformation of the crane’s main beam, wire rope fatigue, broken wire, weld cracking, and ultimately cause heavy objects to fall, the collapse of the whole machine and other major lifting safety accidents.

    Improper load rigging

    The irregular layout of the lifting rigging of the gantry crane is an easily overlooked cause of the falling object accident of the gantry crane, and the safety hazards run through the entire lifting operation process of the gantry crane.Common illegal operations on the site include the use of worn and broken wires, aging and damaged wire ropes and hoisting slings, the mixing of different specifications of spreader accessories, the offset of the center of gravity of the gantry crane hoisting, the angle between the rigging forces is too large, and sharp heavy-duty materials are not protected against cutting and other issues.This kind of hidden danger will not immediately cause equipment failure, but in the dynamic operation process of gantry crane lifting, horizontal translation, and fixed-point blanking, it can easily cause rigging to fall off and fracture, heavy objects to slip off and offset, greatly increasing the risk of high-altitude hoisting and falling objects. It is an important cause of accidents caused by smashing and squeezing injuries by construction site personnel.

    Preventing dropped loads

    Gantry Crane Collisions

    Collisions with structures

    Structural collision accidents of gantry cranes mostly occur in industrial construction scenarios where the site is narrow, multiple gantry cranes cross-operate, and the line of sight of the operation is limited. They are mainly divided into three categories: gantry crane cart walking collision, trolley running sideways collision, and lifting heavy objects swinging collision.During the operation process, the gantry crane in operation can easily hit the plant column, the end limit of the track, the high-altitude pipeline and the surrounding stacking materials, and the swinging lifting heavy objects will also indirectly hit the surrounding machinery and equipment and building structures.Short-term minor collisions will damage the buffer device and walking transmission structure of the gantry crane. Long-term frequent collisions will cause deformation of the steel structure of the gantry crane, track offset, loose fixing bolts, and cause major accidents such as equipment derailment and the collapse of the whole machine. At the same time, it will cause damage to site facilities and delays in the construction period of engineering projects.

    Collisions with personnel

    Man-machine collision of gantry cranes is a high-incidence safety accident with a very high fatality and injury rate, and it is also a key difficulty in on-site safety control of industrial gantry cranes.The flow of personnel on the construction site is complicated, and some construction personnel have weak safety awareness. There are violations such as crossing the equipment operation track, staying in the blind area of gantry crane operation, and following the lifting of heavy objects.At the same time, the gantry crane operators are inattentive in their operations, the surrounding environment is not observed in place, or the construction at night, the haze, sand and dust weather are blocked from sight, making it difficult to find the surrounding operators in time.When multiple equipment cross-operate at close range, insufficient coordination and cooperation of personnel can easily cause secondary collision accidents. The overall burst is strong and the avoidance time is short, which can easily cause personnel to squeeze, crush, and impact injuries.

    Anti-collision systems

    To effectively avoid gantry crane collision safety accidents, it is necessary to rely on the three-in-one gantry crane safety prevention and control plan of intelligent equipment protection, construction site control, and collaborative personnel dispatching.Industrial gantry cranes can be equipped with intelligent anti-collision systems such as infrared sensing and laser ranging, and sound and light early warning and forced shutdown protection are automatically triggered when the equipment is close to obstacles or on-site personnel.The site needs to clean up debris on both sides of the gantry crane track in time, divide the independent hoisting operation area and the personnel passage area, set up eye-catching safety warning signs, and strictly prohibit unrelated personnel from entering the blind area of the gantry crane operation.Multi-equipment cross-operation requires the formulation of special safety plans, standardizing the operating spacing and operating sequence of gantry cranes, the night construction is equipped with lighting equipment, the operation is slowed down in bad weather, and professional personnel are arranged to command and dispatch the whole process.

    Load Swing and Crushing Accidents

    Causes of load swing

    Heavy object swing of gantry cranes is a high-frequency dynamic safety hazard. Uncontrolled load swing can easily cause personnel squeezing and heavy object falling accidents. The risk incentives are mainly divided into three categories: operation, environment, and equipment.Equipment operators start and stop abruptly, change direction at high speed, and uneven translation speed will directly break the force balance of lifting heavy objects; open-air gantry crane operations encounter severe weather such as gusts of wind and side winds, and natural airflow will continue to push heavy objects off the preset lifting trajectory.At the same time, equipment failures such as loose wire ropes, stuck pulleys, and insufficient track flatness of gantry cranes will cause uneven lifting force, forming continuous heavy object swing, and greatly increasing the safety risks of industrial hoisting operations.

    Personnel in danger zones

    The core risk of safety accidents caused by the swing of heavy objects of gantry cranes lies in the illegal detention of on-site personnel in the dangerous operating area of gantry cranes.The swing coverage of heavy objects of gantry cranes, the operating radius of equipment, and the area directly below the hoisting are all restricted areas for high-risk operations, but there are often personnel on the construction site who are lucky enough to cross the gantry crane operation area, and violations such as unreasonable standing positions of command personnel and close-range leaning operations of personnel when the materials are in alignment are very common.Once the suspended lifting heavy objects swing out of control, the on-site personnel cannot quickly avoid them, and safety injuries such as impact, squeezing, and smashing can easily occur. It is the most common personal accident scene in the daily operation of gantry cranes.

    Safe load control

    Precise control of the swing of heavy objects in Henan Mine Crane manufactured gantry cranes to avoid the risk of personnel squeezing requires a combination of standardized operation, operation area control and intelligent lifting equipment assistance.Equipment operators need to start and stop smoothly and at a uniform speed, change direction slowly, eliminate illegal operations such as emergency stop, rapid rotation, and high-speed translation, and predict the trajectory of the operation in advance to weaken the swing of heavy objects.The hazardous operation area of gantry cranes is strictly delineated on site, and personnel are prohibited from entering the swing radius of heavy objects and the blind area of equipment operation, and the material alignment operation is maintained at a safe distance.At the same time, an intelligent anti-swing system of equipment can be installed to dynamically correct the operating trajectory, and the operation of the open-air gantry crane will be stopped immediately in windy and rainy weather, so as to avoid the safety risks of uncontrolled load swing in all directions.

    Gantry Crane Tipping and Structural Failures

    Unstable ground conditions

    The unstable foundation and track foundation are the core hardware hidden dangers of gantry crane overturning and structural failure, which have a great impact on the safety of outdoor operations of large-span gantry cranes and mobile gantry cranes.Uneven soft and hard foundation of the work site, track settlement deformation, excessive flatness, or temporary work ground is not hardened, the backfill soil is not compacted, and the foundation is soaked in water on rainy days, will cause the overall force of the gantry crane to be unbalanced.When the equipment walks to an unstable ground area, the force of the equipment’s outriggers is uneven, the fuselage is tilted, and the hoisting partial load and dynamic load are superimposed, which can easily cause the equipment to roll over and overturn, and it will also cause irreversible structural damage such as distortion of the main beam and cracking of the welds. Structural damage.

    Wind and environmental forces

    Gantry cranes operating in the open air are highly susceptible to environmental factors such as wind, climate, acid-base corrosion, etc., which can cause structural failure and overturning accidents.The horizontal thrust generated by strong winds and gusts of wind will break the balance of force on the equipment, causing the equipment to slip and heavy objects to fall. Most construction site gantry crane overturning accidents are caused by illegal hoisting operations under Category 6 high winds.In addition, rainwater erosion will soften the foundation of the gantry crane operation and corrode the operating track. Coastal salt spray and industrial dust will corrode the steel structure and fastening accessories of the gantry crane, resulting in a decrease in component strength and loose bolts. Extreme low temperatures will also reduce the impact resistance of steel, induce component fracture, and continue to accumulate major safety hazards.

    Structural inspection and maintenance

    Normalized structural inspection and professional maintenance of gantry cranes are the key means to avoid accidents of overturning and structural failure of gantry cranes.Before daily operations, it is necessary to check the compactness of the foundation of the gantry crane and the flatness of the track, calibrate the operating parameters of the equipment track regularly, and repair the hidden areas of settlement, loosening, and water accumulation in time.Strictly implement the wind operation standards of gantry cranes, equipped with professional wind speed detectors, stop immediately in windy weather and lock the windproof anchoring device.Regularly carry out non-destructive testing of the core structures of the main beam, outriggers, welds, connecting bolts, etc. of the gantry crane, timely rust removal and corrosion, replacement of damaged parts, and special investigations before and after bad weather, resolutely prevent equipment from carrying out sick operations.

    gantry crane accidents

    Mechanical and Electrical Failures

    Brake and hoist failures

    The failure of the gantry crane brake system and the hoist lifting system is a high-incidence mechanical hazard, which can easily cause vicious gantry crane safety accidents such as sliding hooks and falling objects.Problems such as brake pad wear, brake spring fatigue, oil leakage from the oil cylinder, and excessive brake clearance of the gantry crane brake system can lead to insufficient braking force and brake failure, causing heavy lifting objects to fall.At the same time, equipment wire rope broken wire rust, pulley caton, reel deformation, insufficient lubrication of the gearbox and other failures will directly lead to lifting power failure and wire rope fracture.Most mechanical failures of gantry cranes originate from the lack of daily maintenance, and minor hidden dangers accumulate for a long time, and eventually evolve into major lifting safety accidents.

    Limit switch malfunctions

    The limit switch is an indispensable core safety protection device for gantry cranes. It is mainly used to limit the operating limit position of gantry cranes and eliminate the safety risks caused by over-range operations.High-frequency mechanical vibration, dust accumulation, rainwater erosion and line aging problems on the construction site are likely to cause equipment limit switches to stall, fail, signal failure, and equipment over-range failure without warning or automatic shutdown.The operator fails to investigate the limit failure of the gantry crane in a timely manner, and the continuous over-range operation will cause the safety hazards of the chain gantry crane such as the hook rushing to the top, the trolley hitting the end, the track derailing, and the wire rope breaking. It is an invisible operation risk that can easily be ignored.

    Electrical system failures

    The failure of the electrical system of the gantry crane is sudden and uncontrollable, which seriously threatens the stability of the operation of the whole machine and the safety of on-site personnel.Dust, humidity, high temperature and continuous mechanical vibration on the construction site can easily cause electrical failures such as aging and damage of equipment cables, short circuit of lines, loose terminal blocks, and failure of contactors.If the fault is light, it will lead to sudden equipment shutdown and failure of operating instructions, and if it is heavy, it will cause dangerous conditions such as equipment malfunction, heavy objects out of control, and electrical fire.At the same time, the gantry crane has poor electrical grounding and insufficient protection, which will cause the risk of leakage and directly threaten the personal safety of the operators.

    Common Human Errors That Cause Gantry Crane Accidents

    Operator mistakes

    More than 70% of gantry crane safety accidents are caused by human error, which is the most important cause of gantry crane accidents.In the operation of gantry cranes on construction sites, operators often experience violations such as overloading and partial-load hoisting based on experience, ignoring the rated load parameters of the equipment, irregular start-stop operation, and forced alignment at high speed.Some personnel are inattentive in their operations, ignoring the hidden dangers of the surrounding environment, forcibly operating with illness after the equipment alarms, and operating lifting equipment in violation of regulations in bad weather and at night.The fault tolerance rate of human error of gantry cranes is extremely low, which is the top priority of safety control on construction sites.

    Poor communication

    Henan Mine Crane manufactured gantry crane hoisting belongs to the collaborative operation of multiple people. Accurate and smooth personnel communication is the basis for safe operation. Omissions in communication can easily induce safety accidents of gantry cranes.Problems such as substandard command gestures, chaotic walkie-talkie channels, and vague hoisting instructions often occur at construction sites. When multiple people cooperate with the operation, the work is unknown and the information is out of sync.Command personnel are improperly positioned and their sight is blocked. It is easy to issue incorrect operation instructions. Under noisy working conditions, the transmission of instructions is biased, and short-term communication errors can cause serious safety consequences such as misalignment of heavy equipment, equipment collisions, and injuries to personnel.

    Inadequate training

    Insufficient job training and lack of professional competence of operators are the root causes of frequent man-made accidents of gantry cranes.In order to reduce costs, some enterprises allow undocumented and inexperienced personnel to operate gantry cranes. Such personnel have not systematically learned the parameters of gantry crane equipment, standardized operating procedures, and on-site hidden danger identification knowledge. Based on simple experience, they cannot accurately judge the risks of various hoisting operations, and the ability to deal with equipment failures is weak.At the same time, the lack of normalization of safety training for gantry cranes, the experiential operation of old operators and the dilution of safety awareness have normalized the illegal operation of equipment, and various safety hazards have continued to accumulate.

    How to Prevent Gantry Crane Accidents

    Daily inspections

    The daily inspection of Henan Mine Crane manufactured gantry cranes is the primary line of defense for investigating hidden dangers in equipment and preventing safety accidents of gantry cranes.Before daily operations, operators need to comprehensively inspect the core components of the gantry crane brake system, winch, wire rope, etc., test the sensitivity of the gantry crane limit device, overload warning, and anti-collision equipment, and investigate the operating safety status of electrical circuits and foundation tracks.After the operation is over, clean the equipment in time, record the hidden dangers of the operation of the gantry crane, report the operating status of the equipment, stop and report for repair immediately if a fault is found, resolutely eliminate the sick operation of the gantry crane, and avoid all kinds of hoisting safety risks from the source.

    Regular maintenance

    Regular maintenance of normalized gantry cranes is the core measure to stabilize equipment performance, eliminate mechanical and electrical failures, and extend the service life of gantry cranes.According to the equipment model, frequency of use, and construction conditions, enterprises need to formulate monthly, quarterly, and annual hierarchical maintenance plans, regularly fill the transmission parts of gantry cranes with special lubricants, and replace worn, aging, and rusted vulnerable parts in time.At the same time, tighten the equipment connection bolts, overhaul the electrical circuits, remove rust and corrosion from the steel structure, calibrate the track accuracy, establish a complete maintenance file, and realize the standardized maintenance of the whole life cycle of lifting equipment.

    Safety devices

    Equipping and standardizing the use of safety protection devices for gantry cranes is a hard guarantee to avoid sudden equipment accidents.Standard industrial gantry cranes need to be equipped with overload limiters, high and low limiters, emergency stop buttons, windproof anchoring devices, sound and light early warning systems and other safety accessories as standard. Open-air gantry cranes are equipped with wind speed monitoring, dust-proof and rain-proof protection facilities, and multi-equipment cross-operation scenarios supporting equipment intelligent anti-collision and intelligent anti-swing systems.Enterprises need to regularly verify the operating accuracy of the protective equipment, and it is strictly forbidden to shield or dismantle the safety equipment privately to ensure the effective operation of the gantry crane’s multiple safety protections throughout the process.

    Clear operating procedures

    Standardized gantry crane operating procedures are the core management basis for standardizing personnel operating behavior, eliminating human error, and reducing the safety accident rate of gantry cranes.Enterprises need to combine their own gantry crane equipment parameters, construction site working conditions and industry safety standards to formulate refined and landing full-process hoisting operation specifications, clarify equipment start-stop, translation, alignment, blanking and other operation details, and clarify various hazardous operation scenarios and prohibited operation regulations.Strictly implement the licensed induction system for gantry cranes, submit safety technology before operation, eliminate overloading, emergency stops and turns, illegal and risky operations, etc., and standardize and standardize the whole process of hoisting operations.

    Emergency response plans

    A sound emergency response plan can effectively reduce casualties and property losses after accidents.Enterprises need to formulate special emergency response plans for various high-incidence accidents such as falling objects, capsizing, collisions, and mechanical and electrical failures, and clarify standardized processes for command and dispatch, personnel evacuation, and equipment rescue.Organize regular emergency drills for all staff to enhance the operator’s fault handling and emergency risk avoidance capabilities, and equip the scene with first aid, windproof, and emergency materials, and quickly start the plan after the accident to control the spread of risks and reduce accident losses.

    Henan Mine Crane Factory Custom

    Most safety accidents of gantry cranes are caused by hidden equipment hazards, environmental impacts, operating errors and management omissions. A good job of full-cycle safety control can effectively avoid risks.As a professional crane manufacturer, Henan Mine Crane Factory is deeply engaged in optimizing the safety performance of equipment, from the core structure, safety configuration to stable quality, and at the same time adapts to various complex working conditions to create high-adaptability and high-safety gantry cranes to help enterprises reduce the risk of failures and accidents from the source of equipment, and ensure the safe, efficient and stable operation of hoisting operations.

    Henan Mine CraneDiscuss your requirements ↗
  • Cleanroom Crane vs Ordinary Crane: Which One Fits High-End Material Handling

    Cleanroom Crane vs Ordinary Crane: Which One Fits High-End Material Handling

    Cleanroom Crane vs Ordinary Crane: Which One Fits High-End Material Handling

    Cleanroom Cranes vs. Standard Cranes: Which Is Better Suited for High-End Material Handling?

    Selecting industrial lifting equipment is never simply a matter of load capacity. The handling of heavy steel in standard factories and the lifting of precision materials in cleanrooms require completely different design standards and operational requirements for Cranes.

    In high-end manufacturing sectors such as semiconductors, biopharmaceuticals, and new energy materials, the core risk of lifting operations is never overloading, but rather material contamination and damage to precision components caused by equipment dust, oil leaks, and operational vibrations. This is also the primary reason why cleanroom cranes are gradually replacing conventional cranes to become standard equipment in high-end cleanrooms.

    Main Application Scenarios for the Two Types of Cranes

    The boundaries between cleanroom cranes and standard cranes are very clear; the production environments, material properties, and operational standards they are suited for differ fundamentally. The core criterion for selection is the project’s production cleanliness grade.

    Semiconductor and Precision Electronics Production Scenarios

    The handling of semiconductor wafers, precision electronic components, and high-end production equipment requires zero tolerance for environmental particulates, impurities, or oil contamination. Even minute dust particles or vibrations can render precision components unusable, directly resulting in significant economic losses.

    In such scenarios, cleanroom Overhead Cranes must be used. Their dust-free and leak-proof design ensures compliance with cleanroom standards throughout the entire process, meeting the safety requirements for handling precision materials.

    Power Battery and Advanced Materials Production Facilities

    Production workshops for lithium battery anode and cathode materials, battery cells and modules, and new energy storage materials are classified as controlled clean environments. Powdered materials are highly prone to absorbing impurities; oil leaks from equipment and metal dust generated during operation can directly affect material purity and product yield rates.

    Cleanroom Cranes are specifically designed for these operating conditions. From structural sealing and lubrication methods to surface treatment, they eliminate the generation of contaminants, making them suitable for the production and handling processes of high-end new energy materials.

    Pharmaceutical and Medical Device Production Scenarios

    The transfer of pharmaceutical raw materials, medical consumables, and sterile production equipment must strictly adhere to pharmaceutical clean production standards. The open structure and exposed lubrication components of ordinary industrial cranes are highly prone to generating contaminants and do not meet the hygiene standards for pharmaceutical production.

    Specialized cleanroom cranes are compatible with pharmaceutical cleanrooms of various grades, maintaining a stable workshop environment throughout the process and mitigating the risk of external contamination.

    Precision Optics and Laboratory Material Handling

    Fragile, high-precision materials such as optical lenses, precision laboratory instruments, and testing equipment not only require a clean environment but also demand extremely stable equipment operation. Even slight vibrations or shaking can cause displacement or damage to precision components.

    Precision handling cranes designed for these scenarios combine dust-free and dust-proof features with low-speed, smooth operation, meeting the specialized high-precision requirements of laboratories and precision optical workshops.

    General-purpose factories and traditional processing workshops

    Traditional industrial settings such as mechanical processing, steel structure manufacturing, and mold production do not have strict particulate matter control requirements. Materials handled are primarily steel, castings, and tooling/molds, with the core requirements being stable load-bearing capacity and durability.

    For these routine lifting operations, standard Overhead Cranes fully meet production needs. These Cranes offer better cost-effectiveness and are well-suited for high-frequency, heavy-load operations in conventional industrial settings.

    Conventional Warehouses and Standardized Production Lines

    The handling and lifting of general warehouse materials and common industrial components do not require stringent cleanliness standards. The focus is on improving handling efficiency and ensuring basic equipment safety; the design standards of standard industrial Cranes are sufficient for these basic operating conditions.

    overhead crane for cleanroom applications

    Core Operational Requirements for High-End Material Handling

    Lifting requirements in high-end cleanrooms differ significantly from traditional industrial lifting. The core focus is no longer simply load-bearing capacity, but rather environmental adaptability and material protection capabilities.

    Extremely Low Contamination Risk Control

    The core challenge in high-end manufacturing is external contamination. During operation, standard cranes can generate metal dust, lubricant mist, and wear debris from components. These microscopic contaminants can directly contaminate precision materials, high-purity materials, and sterile production environments.

    Cranes designed for high-end applications must be comprehensively optimized in terms of structure, components, and lubrication methods to eliminate the generation of various contaminants at the source and maintain a stable cleanroom classification.

    Smooth, Vibration-Free Operation Throughout

    Precision materials and large precision equipment are highly sensitive to vibration and impact. Jerky starts and stops, body swaying, and tracking deviations can all cause misalignment of internal precision structures and damage to materials, resulting in product scrap.

    High-end operating conditions require Cranes to start and stop smoothly, operate at a constant speed, and achieve precise positioning, minimizing mechanical vibration to the greatest extent possible to accommodate high-precision handling operations.

    Dedicated Component Design for Cleanroom Compatibility

    Conventional cranes typically feature open-structure motors, gearboxes, and wire ropes, which are prone to dust accumulation and oil leakage. Cleanroom-specific cranes employ fully enclosed drive systems, dust-proof sealed components, and oil-free lubrication materials, with all exposed parts treated to resist dust and contamination.

    High-Precision Positioning Capability

    Processes such as equipment positioning, material docking, and precision fixture assembly require cranes to possess precise alignment capabilities. Even the slightest positional deviation can affect the assembly precision of the entire production line—a core requirement that standard cranes cannot meet.

    Low-Interference Operation and Maintenance Design

    Downtime costs in cleanrooms are extremely high. Frequent equipment inspections and maintenance not only impact production capacity but also introduce external contaminants. Cranes designed for high-end applications feature durable structures, low failure rates, and simple daily maintenance, ensuring minimal disruption to production processes.

    Adapted to On-Site Production Environments

    Cleanroom classifications vary across industries, as do production workflows and equipment layouts. High-quality lifting equipment must align with the cleanroom class, production processes, and spatial layout, seamlessly integrating into the existing production system.

    Detailed Analysis of Two Crane Models

    Many buyers struggle to distinguish the core differences between these two equipment types, primarily due to a lack of understanding regarding their design objectives: one is specifically engineered for clean, precision applications, while the other is suited for conventional industrial heavy-load scenarios.

    What Is a Cleanroom Crane?

    A cleanroom crane is specialized lifting equipment designed for controlled dust-free workshops and clean production areas, and it is the core model of clean environment cranes. Its design priorities differ entirely from those of ordinary equipment; rather than focusing on maximum load capacity, it prioritizes dust-free operation, contamination prevention, smooth movement, and low vibration.

    The entire unit features a fully enclosed structure, special dust-proof coatings, and a leak-free lubrication system. Components are meticulously selected to ensure that no dust, oil residue, or debris is generated during operation, making it suitable for high-grade cleanrooms in industries such as semiconductors, pharmaceuticals, and new energy.

    What is a standard crane?

    Standard industrial cranes are general-purpose lifting equipment for traditional factory settings, emphasizing heavy-duty capacity, structural durability, and cost-effectiveness. These units feature an open structure with exposed drive components and lubrication systems, allowing for normal mechanical wear and the generation of trace amounts of dust.

    Suitable for industrial environments without cleanliness requirements, this equipment is characterized by simple construction, easy maintenance, and low procurement costs, making it the mainstream lifting solution for traditional manufacturing and warehousing facilities.

    Scenarios Where Cleanroom Cranes Are the Preferred Choice

    Cleanroom cranes are required whenever production areas have specific cleanliness grade requirements, the materials being handled are high-value, or production processes have zero tolerance for contamination.

    This is particularly true in industries such as precision electronics, biopharmaceuticals, and high-purity new materials, where even minute contamination or vibrations can trigger batch-wide quality issues; dedicated cleanroom equipment is the fundamental guarantee for production stability.

    Scenarios Where Standard Cranes Are Sufficient

    For applications such as conventional machining, heavy steel structure handling, warehouse material handling, and general equipment installation/dismantling—where there are no dust-free or precision handling requirements—standard cranes can meet production needs while effectively controlling equipment procurement costs.

    Special Mixed-Use Scenarios

    In certain semi-clean workshops, pre-treatment processes, and non-core clean areas, a full set of high-grade cleanroom cranes is not required. Modified industrial cranes can be selected; by upgrading dust-proof coatings, sealed components, and smooth control systems, they can adapt to semi-clean environments at a lower cost.

    overhead crane for cleanroom applications

    Core Technical Parameters to Verify During Procurement

    The parameter selection logic for these two types of cranes is entirely different. For high-end cleanroom applications, it is not sufficient to simply verify standard parameters; it is essential to focus on specialized indicators such as cleanroom compatibility and operational quality.

    Cleanroom Compatibility Grade

    First, clearly define the nature of the work area: is it a high-grade controlled cleanroom, a semi-clean production area, or a standard industrial zone? Different cleanliness grades require entirely different standards for dust protection, sealing, and contamination prevention, which directly determine the crane model selection.

    Rated Lifting Capacity

    Select the model based on the actual weight of materials, production equipment, and containers, allowing for a reasonable safety margin. Cleanroom cranes are typically suited for handling precision, lightweight materials, whereas standard cranes are designed for heavy-duty lifting; load capacity must be matched to actual operating conditions.

    Equipment Span

    The span must precisely match the width of the workshop or factory building and the production line layout to ensure full coverage of the work area without any lifting blind spots, while avoiding space waste and operational instability caused by excessive span.

    Effective Lifting Height

    Determined by combining equipment installation height, material transfer paths, and workshop clear height, this ensures sufficient space for lifting precision equipment and transferring materials at elevated heights, while preventing operational interference.

    Smooth Operation Performance

    Prioritize verifying the smoothness of hoisting, trolley travel, and overall machine operation. High-quality cleanroom Cranes feature soft start/stop and shock-free operation, effectively reducing body sway and mechanical vibration to protect precision materials.

    Surface Finishing and Material Treatment

    Cleanroom cranes feature a matte, dust-resistant topcoat and a smooth, corrosion-resistant surface that resists dust accumulation, facilitates cleaning, and prevents flaking or debris shedding. Conventional cranes prioritize rust prevention and load-bearing capacity, with surface treatments that do not require dust or stain resistance.

    Lubrication and Sealing Design

    Cleanroom models feature a fully enclosed lubrication system and leak-proof sealing structures, ensuring grease does not spill and that no dust is released from component wear. Standard Cranes use open lubrication systems, which cannot prevent oil leaks or the release of wear dust.

    Control Methods

    Cleanrooms typically use wireless remote control and precise electronic control modes, offering fine-tuned operation and accurate positioning to accommodate precision tasks. For standard applications, joystick control is sufficient to meet basic lifting requirements.

    Ease of Maintenance

    Maintenance in cleanroom areas must be completed quickly to minimize environmental disruption. Cleanroom Cranes feature an optimized component layout with centralized maintenance points, enabling rapid repairs and replacements to reduce downtime.

    Core Differences Between Cleanroom Cranes and Standard Cranes

    While the two types of equipment appear structurally similar, they differ significantly in core design, application scenarios, and value—key factors that must be clearly understood when selecting equipment for high-end projects.

    Differences in Environmental Adaptability

    Cleanroom cranes are specifically designed for controlled environments that are dust-free, sterile, and low in particulate matter, enabling long-term, stable operation in various high-grade cleanrooms. Standard cranes are only suitable for ventilated, open conventional industrial facilities and cannot operate within cleanroom areas.

    Differences in Contamination Control Levels

    Cleanroom models implement comprehensive contamination control across components, lubrication, coatings, and structure, ensuring zero dust, zero oil residue, and zero debris throughout the entire process. Standard cranes lack contamination control design; mechanical wear and grease leakage during operation generate contaminants.

    Differences in Structure and Component Craftsmanship

    Cleanroom cranes utilize precision-sealed components, specialized dust-proof coatings, and low-wear core parts, featuring meticulous craftsmanship and stringent material standards. Standard cranes prioritize structural strength and heavy-load capacity, with component manufacturing standards better suited to conventional industrial needs.

    Differences in Operational Quality

    Cleanroom models feature more precise electronic control systems, ensuring smooth starts and stops, minimal vibration, and high positioning accuracy—ideal for handling precision materials. Standard Cranes exhibit significant operational inertia and noticeable sway, making them unsuitable for high-precision, high-protection material handling requirements.

    Differences in Purchase Costs

    Due to precision manufacturing, specialized components, and dust-free design, cleanroom cranes carry a higher purchase price than standard industrial cranes. Standard models feature simple structures and mature manufacturing processes, offering a clear cost-effectiveness advantage.

    Differences in Lifecycle Value

    In cleanroom environments, high-cost cleanroom cranes eliminate the risks of material contamination and product scrap, thereby reducing production losses. While standard cranes are lower in price, they are prone to quality incidents, resulting in higher overall costs over the long term.

    How to Select a Reliable Crane Supplier

    The customization requirements for cleanroom lifting equipment are far higher than those for standard cranes. Many manufacturers lack design experience in cleanroom environments, making it highly likely that equipment will fail to meet compatibility standards.

    Verify the Manufacturer’s Design Experience in Cleanroom Environments

    Many manufacturers specialize only in standard industrial cranes and are unfamiliar with the dust-proof, contamination-proof, and low-vibration design standards required for cleanrooms. Prioritize manufacturers with deep expertise in cleanroom environments for the semiconductor, pharmaceutical, and new energy industries to ensure equipment compatibility.

    Review Completed Projects in Similar Fields

    Focus on the manufacturer’s completed projects in precision manufacturing, biopharmaceuticals, and new energy materials. Authentic project experience is the best testament to equipment quality and adaptability.

    Assess Professional Engineering Customization Capabilities

    High-quality manufacturers can optimize equipment structure, sealing methods, and electrical control systems on a one-to-one basis according to the cleanroom class, material characteristics, and production line layout, creating customized solutions tailored to project requirements.

    Verify Complete Set of Technical Documentation

    Reputable manufacturers provide a full set of documentation, including assembly drawings, surface treatment specifications, operating parameter manuals, sealing structure descriptions, and maintenance guidelines, to meet the acceptance and operational standards of high-end projects.

    Confirm Selection Criteria for Core Components

    Motors, gearboxes, brakes, seals, cables, and lubricants for cleanroom cranes all have specific standards. Each component selection must be verified individually to prevent the use of generic substitutes.

    Clarify Equipment Testing and Commissioning Standards

    Before leaving the factory, cleanroom equipment must undergo stability testing, dust-proof sealing inspections, precision alignment adjustments, and no-load and full-load trial runs to ensure it can immediately adapt to clean production conditions upon arrival at the site.

    Verify After-Sales and Spare Parts Support Capabilities

    High-end clean production lines cannot tolerate prolonged downtime. Manufacturers must provide rapid after-sales response, dedicated spare parts inventory, and dust-free maintenance services to minimize losses from production interruptions.

    overhead crane for cleanroom applications

    Common Misconceptions in Procurement and Selection

    Many equipment compatibility issues in high-end projects stem from cognitive biases during the selection phase. Seemingly minor errors can directly impact product yield rates and production stability.

    Using price as the sole selection criterion and substituting standard Overhead Cranes for cleanroom-grade equipment to cut costs ultimately leads to serious issues such as material contamination and batch scrapping.

    Assuming all Overhead Cranes perform identically and ignoring the specific requirements of cleanroom environments—such as dust prevention, contamination control, and low vibration—results in equipment that cannot be put into service upon arrival.

    Failing to clarify the specific cleanliness grade of the workshop and selecting equipment blindly leads to a mismatch between equipment standards and on-site conditions.

    Ignoring hidden risks such as equipment leaks, dust generation, and contamination during operation and maintenance, while focusing solely on basic lifting functions.

    Over-specifying equipment—purchasing high-grade cleanroom Cranes for standard semi-clean environments—results in wasted equipment costs.

    Selecting under-specced equipment for high-precision, high-cleanliness processes creates potential quality hazards.

    Choosing manufacturers with no experience in cleanroom projects leads to equipment designs that fail to meet high-end production standards.

    Equipment parameters do not align with production line workflow design, resulting in low operational efficiency and poor adaptability.

    Frequently Asked Questions

    What is the core difference between cleanroom cranes and standard cranes?

    The core difference lies in their design objectives. Cleanroom cranes prioritize dust-free operation, contamination prevention, low vibration, and high precision, making them suitable for high-end cleanroom and precision applications; standard cranes prioritize heavy-duty capacity and durability, making them suitable for conventional industrial lifting tasks, without cleanroom protection features.

    Does all high-end material handling require cleanroom cranes?

    No. Only materials that are contamination-sensitive, precision-sensitive, fragile, or high-value require cleanroom equipment. For general high-end heavy-duty equipment or precision handling without cleanroom requirements, modified industrial cranes can be used.

    Are cleanroom cranes always more expensive?

    Yes. Dedicated dust-proof sealing processes, precision electronic controls, high-quality components, and refined production workflows all increase equipment costs. However, the production stability and quality assurance they provide are irreplaceable by standard equipment.

    Which industries must use cleanroom-grade Cranes?

    Industries such as semiconductors, precision electronics, biopharmaceuticals, power batteries, high-purity new materials, and precision optical laboratories must use cleanroom Cranes to ensure production environment integrity and material quality.

    Can standard cranes be retrofitted for cleanroom environments?

    Only semi-clean or low-demand environments can undergo simple dust-proof retrofits. High-grade cleanrooms cannot be retrofitted as substitutes; factory-customized cleanroom-specific cranes must be selected.

    What information should be provided to the manufacturer before requesting a quote?

    The workshop’s cleanroom class, maximum material weight, required span and lifting height, workshop layout drawings, and production process requirements—to enable the manufacturer to provide a precise customized solution.

    How do you determine whether a project requires a complete set of cleanroom equipment or modified industrial equipment?

    This determination is based on the facility’s official cleanliness grade, material contamination sensitivity, and production process standards. High-grade cleanrooms and core precision processes require a complete set of cleanroom equipment, while auxiliary processes may use modified models.

    overhead crane for cleanroom applications

    Summary

    There is no absolute superiority between cleanroom cranes and standard cranes; the distinction lies solely in their suitability for specific operating conditions. In traditional heavy-duty industrial settings, standard cranes offer better value for money; in high-end cleanroom and precision material handling scenarios, cleanroom cranes are the core equipment for ensuring product quality and stable production.

    When selecting equipment, one should not focus solely on price and load capacity parameters, but rather make a comprehensive assessment that considers the workshop’s cleanliness grade, material properties, production processes, and long-term production plans. Overspecifying equipment leads to wasted costs, while underspecifying it can result in serious production risks.

    Henan Mine Crane specializes in the R&D and customization of cleanroom lifting equipment. With extensive experience in implementing high-end projects in the semiconductor, pharmaceutical, and new energy sectors, we can tailor high-end material handling Crane solutions to meet specific cleanroom requirements, complete with comprehensive technical documentation and long-term after-sales support.

    If you are unsure whether your project requires a cleanroom crane or a standard crane, please provide details on material types, load requirements, workshop cleanliness standards, and site drawings. Our engineering team will then provide you with a precise selection proposal.

    Henan Mine CraneDiscuss your requirements ↗
  • Choosing the Best Gantry Crane for Outdoor Stockyards & Material Handling

    Choosing the Best Gantry Crane for Outdoor Stockyards & Material Handling

    Choosing the Best Gantry Crane for Outdoor Stockyards & Material Handling

    The demand for outdoor heavy-duty handling in steel depots, docks, shipyards, construction sites and logistics hubs continues to rise.Under the demand of the industry to improve quality, reduce costs and increase efficiency, traditional equipment cannot be adapted to high-intensity open-air operations, and harsh working conditions such as wind, rain, sand, dust, corrosion, etc. can easily cause equipment failures and affect operating efficiency, and there are safety risks.

    Relying on an independent floor-to-ceiling support structure, outdoor gantry cranes are perfectly adapted to open-air operation scenarios. They have core advantages such as wide coverage, strong carrying capacity, and stable operation. They are the core equipment for material handling in outdoor depots, which can effectively improve the operating capacity, construction safety and overall operating efficiency of enterprises.

    The model parameters of gantry cranes are complicated, and blind purchase is prone to problems of poor adaptability, idle equipment, and high operation and maintenance costs.This article systematically explains the relevant knowledge, applicable scenarios, selection methods, procurement misunderstandings and industry trends of outdoor gantry cranes, so as to help enterprises accurately select models and purchase cost-effective products.

    What Is an Outdoor Gantry Crane?

    Outdoor gantry crane is a ground-supported open-air lifting equipment. It does not need to rely on the building structure of the factory building. It relies on its own outriggers to land firmly. It can stand across the outdoor work area to complete the three-dimensional handling of heavy materials. It is an efficient lifting equipment exclusive to the outdoor yard.

    Its core structure is simple and precise, and the five core components work together to complete the operation.:

    • Main beam: The core load-bearing beam spans the operating area and carries all the loads of the trolley, lifting mechanism and cargo. It is divided into two mainstream structures, single beam and double beam.
    • Support legs: vertical steel structure brackets, connecting the main beam and the ground walking mechanism, are the basis for the independent operation of the equipment and ensure the stability of the operation of the whole machine.
    • Lifting mechanism: it consists of electric hoist, wire rope reel, hook and other components. It is responsible for the vertical lifting of goods and is the core power component.
    • Trolley operating mechanism: A walking trolley mounted on the top of the main beam can drive the goods to move laterally along the main beam, covering the horizontal working area.
    • Cart operating mechanism: A walking device installed at the bottom of the outriggers drives the entire crane to move vertically along the ground track or the ground to expand the vertical operating range.

    Relying on the linkage operation of the three dimensions, the gantry crane can realize vertical lifting, horizontal translation, and vertical walking of cargo, covering the outdoor yard operation area in all directions, and accurately completing the loading, unloading, transshipment, and stacking of various heavy materials.

    The core difference between gantry cranes and bridge cranes

    It is easy for many users to confuse gantry cranes with bridge cranes. The operating principles of the two are similar, but the structural support, installation scenarios, and applicable environments are greatly different. They are the core distinguishing points of the selection. The specific comparison is as follows:

    Contrast dimension Gantry crane Bridge crane
    Support structure Independent outrigger support on the ground, no need for building support Relying on the track system of the plant building, the supporting building structure is required
    Installation adaptability Designed for outdoor scenes, open-air installation without pressure Only suitable for indoor use, relying on closed plant structure
    Core application scenarios Outdoor yard, port terminal, open-air construction site, steel material yard Indoor workshop, factory production line, closed processing site
    Environmental adaptability Weather-resistant, corrosion-resistant, and suitable for complex outdoor working conditions Only suitable for indoor constant temperature, dry, no exposure to rain and rain environment

    In summary, gantry cranes are the only suitable professional equipment for outdoor and open-air material handling scenarios. There is no need to transform the factory building, the infrastructure cost is lower, and the scene adaptability is stronger.

    Common Applications of Gantry Cranes in Outdoor Stockyards

    With its strong outdoor adaptability and heavy-duty operation capabilities, gantry cranes are widely used in various outdoor heavy-duty material handling scenarios, covering many industries such as industry, logistics, infrastructure, and shipbuilding.

    Steel and metal raw material yard

    The heavy weight, miscellaneous types and dense stacking of materials in the steel yard are the core application scenarios of gantry cranes.The equipment can accurately handle all kinds of heavy metal materials, including steel coils, steel plates, steel pipes, I-beams, channel steel and other profiles, and is suitable for the whole process of steel storage, transportation, loading and unloading.

    With special spreaders (C-type spreaders, magnetic cranes, balance beams, etc.), steel deformation and surface wear can be effectively avoided, labor and forklift operations can be greatly replaced, and yard regularity and operating efficiency can be improved. It is the core standard equipment of steel processing and warehousing enterprises.

    Container and logistics terminal

    In container terminals and large logistics hubs, gantry cranes undertake the core container loading, unloading, stacking, and transshipment work.The equipment can efficiently complete the cargo transfer between containers and trucks, ships, and depots, increase the density of container stacking through standardized operations, maximize the use of yard space, and solve the pain points of traditional logistics depots with large footprint, low storage capacity, and slow turnover.

    At present, the modern intelligent terminal has realized the automated operation of gantry cranes, connected to the terminal operation and maintenance system, and completed unmanned, high-frequency and high-precision container handling operations.

    Material handling on construction sites

    The working conditions of the infrastructure construction site are complex and the operating area is dynamically changing. With the advantages of mobility and adaptability, the gantry crane is perfectly adapted to the construction scene.It is mainly used for handling materials such as precast concrete components, steel structure frames, large machinery parts, and heavy construction equipment.

    The equipment can flexibly adjust the operating position according to the construction progress, and the installation and disassembly are convenient, and it is suitable for all kinds of large-scale infrastructure projects, road and bridge projects, and assembled building construction scenarios.

    Shipyard and port operations

    The shipyard has the industry’s top heavy-duty operation requirements. The weight of materials such as hull segments, ship main engines, and deck equipment can reach hundreds of tons, and the carrying capacity, stability, and accuracy of lifting equipment are extremely demanding.Heavy-duty gantry cranes (gantry cranes) are the core equipment of shipyards, which can complete the hoisting, splicing, and transshipment of ultra-large components.

    At the same time, port bulk cargo and heavy equipment loading and unloading operations also rely on heavy-duty gantry cranes to complete all-weather, high-intensity outdoor heavy-duty operations.

    Key Factors When Choosing the Best Gantry Crane for Outdoor Use

    Selection is the core link that determines the operating efficiency, service life, and safety of equipment. Enterprises need to combine their own working conditions to accurately match the four dimensions of load, span, model, and operating parameters to avoid selection errors.

    Determine the rated lifting load

    Lifting tonnage is the first core parameter of selection. Insufficient load will cause safety hazards, while excess load will cause equipment to be idle and costs to be wasted.According to the operating load, it can be divided into three categories:

    • Light-load type (1-10 tons): Suitable for light-load, low-frequency outdoor operation scenarios such as small outdoor depots, equipment maintenance, and light material handling.
    • Medium-load type (10-50 tons): suitable for small and medium-sized factory depots, ordinary logistics transshipment and conventional steel storage, and can stably cope with daily high-frequency medium-load operations.
    • Heavy-duty type (more than 50 tons): Designed for large steel mills, ports, docks, shipyards, and key infrastructure projects, it can be competent for large-tonnage, high-load, and all-weather continuous heavy-duty operations.

    When selecting the type, it is necessary to focus on the three indicators of rated lifting weight, maximum cargo weight, and safety factor. When calculating the load, it is necessary to include the weight of spreaders, beams and other accessories. It is recommended to reserve 15%-25% of the load margin to adapt to the needs of future production capacity upgrades, strictly follow industry safety standards, and eliminate hidden dangers of overload operations.

    Adapt to span and work site size

    The shape parameters of the crane directly determine the coverage of the operation, and it needs to be fully adapted to the layout of the yard, the material stacking method, and the operation movement line to avoid blind spots in the operation.The core parameters include:

    • Span: Refers to the distance between the centers of the tracks on both sides, which needs to match the maximum working width of the yard, taking into account the material stacking and vehicle passage space, and eliminating the problem of restricted operations.
    • Lifting height: For the maximum vertical lifting stroke of the hook, it is necessary to meet the height requirements of material stacking and vehicle loading and unloading, and reserve sufficient safe avoidance distance to ensure the safety of operations.
    • Track operation length: Determine the vertical operation coverage of the crane, it is necessary to completely cover the core operation area of the yard, and reserve a safety buffer zone at both ends of the track.

    Before selecting the type, it is recommended to survey the site on the spot, and customize the exclusive size parameters based on the layout of the yard, the height of the material stacking, and the operation movement line to ensure full coverage of the equipment operation, no dead ends, and no redundant waste of performance.

    Optimal adaptation model

    The mainstream outdoor gantry cranes on the market are divided into four major models. The structure, performance, and adaptation scenarios of different models are significantly different, and the working conditions need to be accurately matched.:

    Single beam gantry crane

    Using a single main beam structure, the structure is simple, the cost is low, and the maintenance is convenient. It mainly focuses on light and medium-load operations.Suitable for 1-20 tons of light material handling, suitable for outdoor depots with limited budgets, medium operating frequencies, and small loads, small processing plants, and equipment maintenance scenarios.The core advantages are high cost performance, convenient installation, and low late operation and maintenance costs.

    Double girder gantry crane

    The symmetrical structure of the double main beam has stronger bearing capacity, higher stability, greater lifting height and longer service life. It mainly focuses on heavy-duty and high-frequency operations.Suitable for heavy-duty material handling of more than 50 tons, it is widely used in high-intensity operation scenarios such as large steel depots, ports, heavy industry manufacturing, shipyards, etc., and can cope with 24-hour continuous operation with excellent safety and stability.

    Rail gantry crane (RMG)

    Relying on fixed track operation, it has extremely high positioning accuracy, stable operating efficiency, supports automated control, and focuses on standardized and high-turnover operations.It is mainly used in container depots, large-scale logistics hubs, and standardized storage parks. It is suitable for large-scale, intelligent, and high-frequency batch material transfer operations. It is the core standard equipment of intelligent terminals.

    Tire gantry crane (RTG)

    It uses rubber tires to walk without laying a fixed track, can move freely and flexibly, and has strong adaptability to the site.It is suitable for outdoor scenes where the operating area is not fixed and the operating points need to be switched frequently. It is mostly used for temporary container transshipment and material handling in scattered depots. There is less investment in infrastructure and full operating flexibility.

    Outdoor Gantry Crane Features for Harsh Environments

    Outdoor harsh environments such as wind, rain, exposure, dust, corrosion, and strong winds require much higher weather resistance, safety, and stability of cranes than indoor equipment. Special outdoor configuration is the key to the long-term operation of the equipment.

    All-weather weather protection design

    • Anticorrosive steel structure: high-grade weather-resistant steel is used, and it is equipped with hot-dip galvanized and multi-layer anticorrosive coating technology for corrosion scenarios such as seaside and chemical industry to eliminate rust, aging, and structural deformation.
    • Waterproof electrical system: electrical components such as motors, control cabinets, junction boxes, etc. adopt IP55/IP65 advanced waterproof and dustproof protection levels to prevent rain and dust intrusion and avoid circuit failures.
    • Wind-resistant and stable design: equipped with special windproof rail clamps and anchoring devices, the structure has been verified by wind load, which can withstand strong winds and weather, prevent equipment from slipping and overturning, and adapt to open-air windy conditions.

    A full set of intelligent security protection system

    Outdoor heavy-duty operations have complex working conditions and high safety risks. A full set of intelligent safety protection systems can avoid hidden dangers in operations in all directions and ensure the safety of personnel, goods and equipment. The core configuration functions are as follows:

    • Overload protection device: real-time dynamic monitoring of heavy loads, once the rated load is exceeded, the equipment will automatically be powered off and shut down immediately, and equipment damage and safety accidents caused by overload operations will be eliminated from the source.
    • Emergency stop system: The whole machine is equipped with an emergency stop button in the whole area. When encountering emergencies such as sudden failures and personnel hazards, the power of the equipment can be cut off with one key, and the equipment can be stopped quickly to avoid risks and minimize operating risks.
    • Stroke limit switch: accurately control the limit operating stroke of the hook lifting and walking of the whole machine, effectively eliminate equipment collisions, structural deformation, damage to accessories and other problems caused by over-range operation, and ensure the safety of the operation boundary.
    • Anti-collision device: adapted to multi-device collaborative operation scenarios, real-time identification of equipment spacing through intelligent sensing, automatic deceleration, limit, and shutdown operations, effectively avoiding equipment collision failures and secondary safety hazards.

    Intelligent electronic control and operating system

    • Wind speed monitoring system: monitor the wind speed of the outdoor environment in real time 24 hours a day. When the wind speed exceeds the safe operating threshold, the system automatically alarms and locks the equipment, prohibits illegal operations, and effectively protects against the risk of overturning and slippage caused by strong winds.
    • The modern outdoor gantry crane is equipped with an intelligent electronic control system, which is upgraded from multiple dimensions of control accuracy, operation convenience, and operation stability, and is fully adapted to the needs of efficient and safe intelligent yard operations. The core configuration advantages are as follows:
    • Frequency conversion drive system (VFD): To achieve smooth start and stop of equipment and stepless speed regulation, to eliminate job shocks and material shaking, and to accurately control the operating speed, not only to protect the integrity of equipment and goods, but also to effectively reduce energy consumption.
    • Remote control + ground operation dual control mode: compatible with wireless remote control and ground operation, operators can avoid blind spots in the operation, stay away from high-risk operation areas, and improve the construction safety factor in all directions.
    • PLC intelligent automation system: supports custom preset operating processes, can realize standardized semi-automatic and fully automatic operations, and is suitable for large-scale, normalized and efficient operation scenarios of smart depots.
    • Real-time intelligent monitoring system: continuously monitor core data such as equipment load, temperature, vibration, and operating status 24 hours a day, accurately predict potential failures, and realize early investigation of hidden dangers.

    The complete set of intelligent electronic control system can effectively reduce the intensity of manual operation, avoid human operation errors, and greatly improve the accuracy and operating efficiency of material hoisting. At the same time, it reduces equipment loss and extends the service life of the whole machine, helping enterprises to achieve efficient, stable and low-cost normalized outdoor lifting operations.

    Gantry Crane Specifications Buyers Should Compare

    When comparing the quotations and plans of various manufacturers, it is important not to only look at the total price. It is necessary to check the parameters one by one and the specifications one by one, so as to effectively avoid the procurement pitfalls such as low-price allocation, false parameter bids, and shrinking configuration.The following is a checklist of the core parameters necessary for procurement acceptance:

    Mechanical core parameters

    During the procurement verification phase, it is necessary to focus on checking a number of core mechanical parameters, including the rated lifting weight, the span of the whole machine, the maximum lifting height, the working level of the equipment, the operating work system, the effective walking length of the track and the weight of the whole machine.

    Among them, the rated lifting weight determines the upper limit of carrying capacity, the span and lifting height determine the coverage of the operation, and the working level and working system are adapted to the needs of outdoor high-frequency heavy-duty operations.Accurate verification of various parameters can ensure that the performance of the equipment fits the on-site working conditions, and effectively avoid problems such as restricted operations, equipment overload and wasted performance.

    Electrical core parameters

    The verification of electrical parameters covers the rated power of the motors of various institutions, the control method, the adaptation voltage of the equipment, the electrical protection level, the frequency conversion speed regulation configuration and the brake system specifications.The full set of electrical configuration needs to match the power supply conditions of the factory area to ensure that the whole machine has stable control, accurate response, and insulation protection up to standard, and fully meets the safe electricity consumption specifications for complex outdoor working conditions.

    Structural process parameters

    During the procurement phase, it is necessary to strictly verify the main steel specifications, anti-corrosion process system, coating thickness standards, equipment design specifications and welding process parameters, and review the complete factory quality inspection report and certificate of conformity one by one to ensure that the whole machine has solid structural strength, excellent outdoor corrosion and weather resistance, and all technical indicators are strictly in line with industry standards and safety specifications.

    Common Mistakes When Buying an Outdoor Gantry Crane

    Most companies are prone to falling into low-cost misunderstandings when purchasing, which leads to frequent failures in the later stage, soaring operation and maintenance costs, and security risks. The four high-frequency misunderstandings must be avoided:

    Ignore cost performance

    Low-cost equipment generally has problems such as thin steel materials, poor-quality accessories, rudimentary technology, and lack of safety configuration.Short-term procurement costs are low, but long-term problems such as high failure rate, frequent downtime, high maintenance costs, and short service life will occur. The comprehensive operating cost far exceeds that of high-quality equipment, and there are great safety risks.Procurement needs to focus on the whole life cycle cost, rather than a single purchase price.

    Ignore the on-site working conditions and environment

    The temperature, wind, humidity, dust, and degree of corrosion in different regions vary greatly.Seaside docks need to strengthen anti-corrosion and windproof configurations; industrial and mining dust scenes need to strengthen dust-proof seals; low-temperature areas need to be adapted to cold-resistant steel and lubricants.Ignoring the customization of working conditions will lead to rapid aging of equipment and frequent failures.

    Improper selection of lifting tonnage

    Small tonnage selection will lead to long-term overload operation of equipment, resulting in structural deformation, wear and tear of accessories, and sudden loss of life, which can easily cause safety accidents; excessive tonnage selection will cause equipment to be idle, energy consumption is too high, and funds are wasted.It is strictly forbidden to select the type according to the average load, and it must be accurately configured according to the maximum load + safety margin.

    Ignore after-sales supporting services

    Gantry cranes are large-scale industrial equipment, and lifetime operation and maintenance, parts replacement, and fault repair are essential.Some small manufacturers do not have a perfect after-sales system, and accessories are difficult to find and no one repairs after equipment failure, and the loss of long-term downtime far exceeds the equipment price difference.Be sure to verify the manufacturer’s technical support, parts supply, and on-site service capabilities before purchasing.

    How to Choose a Reliable Gantry Crane Manufacturer

    High-quality equipment comes from reliable manufacturers. After the selection is over, the strength of the manufacturer is the core of ensuring the quality, after-sales and service life of the equipment. It can be assessed from four dimensions.:

    Manufacturing strength

    Inspect the manufacturer’s production plant, CNC processing equipment, welding technology, and quality inspection system, and confirm that the manufacturer has an independent design, production, processing, and testing team, with the ability to mass produce and customize large-scale gantry cranes, and eliminate OEM and small workshop manufacturers.

    Authoritative qualification certification

    Regular manufacturers must have authoritative qualifications such as lifting equipment production qualification, ISO quality system certification, and CE certification. The equipment strictly follows industry standards such as FEM, ISO, and national standard, and has a complete factory inspection report and certificate of conformity to ensure equipment compliance, safety, and compliance.

    Customized design ability

    High-quality manufacturers can provide one-stop services for free site survey, working condition analysis, personalized program customization, drawing design, and installation guidance. Non-standard equipment can be customized for special sites and special working conditions, rather than forcibly applying standard models.

    Perfect after-sales system

    Reliable manufacturers provide a full set of services such as equipment commissioning, operator training, regular maintenance, lifetime parts supply, and 24-hour technical support. They have the ability to quickly repair on-site and minimize equipment downtime.

    Conclusion

    Outdoor gantry cranes are widely used in ports, depots, engineering construction and other scenarios. The selection is directly related to the operating efficiency, production safety and operating costs of enterprises.Enterprise procurement cannot only value low prices. It needs to take into account the actual working conditions, and comprehensively consider the lifting weight, span, working level, weather resistance, safety configuration and later expansion needs.

    Gantry cranes adapted to outdoor working conditions need to have reliable structural performance and operating stability, while adapting to complex environments such as wind and rain, corrosion, and temperature differences.Choosing a manufacturer with professional design capabilities and a perfect service system can reduce the equipment failure rate, ensure stable production, and improve the cost performance of the whole life cycle of the equipment.

    Henan Mine Crane specializes in providing gantry, bridge, port lifting equipment and intelligent lifting solutions. It can combine customer site, handling and industry needs to provide integrated customized services for program design, equipment manufacturing, and technical support, relying on mature project experience and strict quality control to ensure that the equipment is adapted to various working conditions.

    Henan Mine CraneDiscuss your requirements ↗