Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

分类: Technical Resources

Crane selection, technology, operation and purchasing knowledge.

  • How to Choose a Casting Crane for Molten Metal Handling?

    How to Choose a Casting Crane for Molten Metal Handling?

    How to Choose a Casting Crane for Molten Metal Handling?

    In the steel mill, metallurgical plant for a long time, we all know how high the risk of molten metal operations – a spoonful of thousands of degrees Celsius of steel, iron, relying on casting cranes (also known as ladle cranes) transit, which is the metallurgical workshop’s “lifeline”. Choose the right one, can guarantee decades of safe and stable operation; choose the wrong one, not only will frequent downtime delay production, more likely to trigger steel leakage, equipment collapse and other catastrophic accidents.

    I do in Henan Mine Crane metallurgical crane sales and technical support for more than twenty years, I have seen too many steel mills because of selection errors stepped on the pit: some in order to save costs, instead of a special casting crane with an ordinary bridge crane, less than two years on the steel structure deformation; some underestimated the intensity of the operation, selected the low level of equipment, frequent braking failures, the monthly downtime loss of tens of thousands of dollars.

    Today, I will take the perspective of a line of engineers, the molten metal operation with casting crane selection points, dismantled clearly. Do not talk about false theories, only practical experience, to help you avoid common misunderstandings, and choose the equipment that is really suitable for steel plant conditions, while taking into account the safety, durability and cost-effective.

    What Is a Casting Crane for Molten Metal Handling?

    Simply put, a casting crane for molten metal handling is a heavy-duty double girder overhead crane designed specifically for lifting and transferring molten metal ladles. The biggest difference between it and ordinary overhead cranes lies in the whole design around the “safe, stable, high temperature”, the core function is in the steel mill converter, refining furnace, continuous casting machine, smooth transfer of steel, iron, taking into account the auxiliary lifting equipment maintenance.

    Typical Applications

    Casting cranes are used in almost the entire metallurgical industry, with the core focus on the transfer of molten metal, each of which has extremely high requirements for the safety and durability of the equipment.

    Steelmaking workshop (BOF/EAF converter) is the most important application scenario, responsible for the converter smelting steel, transferred to the refining furnace or continuous casting machine, every day to withstand dozens of high-frequency lifting, is an indispensable core equipment in the production process of steel mills.

    The secondary refining workshop (LF/RH refining furnace) is also inseparable from it, mainly used for lifting the steel after refining, as well as the auxiliary materials required in the refining process, the work requires higher precision to avoid the steel shaking caused by the composition of uneven.

    Continuous casting area of the casting crane, responsible for lifting steel to the continuous casting machine crystallizer, but also with the rhythm of continuous casting, to achieve continuous, smooth supply of steel, once the equipment failure, the entire continuous casting production line will come to a standstill.

    In addition, non-ferrous metal metallurgical plants (such as copper, aluminum smelting), will also use casting cranes, lifting non-ferrous molten metal, suitable for different melting points, different corrosive molten metal operation needs.

    Working Environment Characteristics

    Understanding the working environment of casting cranes, in order to understand why it needs a special design – the working environment of steel mills, known as the crane’s “extreme testing ground”, every feature is testing the performance of the equipment.

    High temperature and heat radiation is the most intuitive challenge. Steel temperature can reach more than 1600 degrees Celsius, cranes operating in this environment for a long time, the main beam, outriggers and other steel structures will be continuously baked, electrical components will also face high-temperature aging problems, ordinary crane components will not take long to fail.

    Dust, smoke and corrosive gases should not be ignored. Steel smelting process will produce a lot of dust, fumes, these dust will enter the mechanical gaps in the equipment, electrical wiring, accelerating the wear and tear of components; corrosive gases will corrode the metal structure and electrical components, reducing the service life of the equipment.

    More critical is the high-frequency, high-load continuous operation. Casting cranes in large steel mills are basically running 24 hours a day, and the number of lifting times per day can reach dozens of hundreds of times, which is in full load or even overloaded state for a long time, which is a great test for the rigidity of the structure of the equipment, the braking system, and the transmission system.

    Why Casting Cranes Require Special Design

    Many customers ask me why casting cranes are so much more expensive than ordinary cranes, which are also overhead cranes. The answer is simple – it is not an ordinary lifting equipment, but is customized for high-risk operations such as molten metal, and every part of its design is designed to cope with the extreme working conditions to ensure safety and durability.

    High Safety Requirements

    When working with molten metal, even a one-in-a-million malfunction can cause irreversible consequences – steel leakage can cause fires and burns, and equipment collapse can lead to casualties and huge property losses. Therefore, the safety requirements of casting cranes, far more stringent than ordinary cranes, must be equipped with multiple redundant safety systems.

    For example, the braking system, ordinary cranes only a set of brake is enough, but casting cranes must be equipped with a double independent braking system (mechanical brake + electromagnetic brake), even if one set of brake failure, the other can be timely braking equipment to ensure that the ladle will not fall. This is the core requirement of molten metal crane safety features.

    When Henan Mine Crane designs casting cranes, it also adds multiple safety configurations such as overload protection, rope breakage protection, anti-decoupling device, etc. Each safety component has been strictly tested to ensure that it can work properly under extreme conditions, eliminating potential safety hazards from the root.

    Heavy-Duty Operation

    The work intensity of casting cranes is incomparable to that of ordinary cranes, which requires it to reach a higher level of work. The industry standard is very clear, molten metal operation with casting cranes, the working level is usually FEM A7-A8, ISO M7-M8, CMAA Class E-F, which is also the core application of FEM A8 crane classification. Scenario.

    Many customers will underestimate the importance of the working class, thinking that as long as the lifting capacity is enough, the low working class equipment can be used. Previously, there is a medium-sized steel mills, selected FEM A6 level of casting cranes, used in the converter shop steel lifting, less than a year on the deformation of the main beam, gear box wear and tear serious problems, the monthly maintenance costs increased by tens of thousands of dollars, and finally can only be replaced in advance of the equipment, but spent more money.

    FEM A7 class is suitable for high-frequency, medium-heavy-duty operations, such as refining workshop; FEM A8 class is suitable for 24-hour continuous, high-heavy-duty operations, such as large converter workshop. Henan Mine Crane’s casting cranes are designed according to A8 class by default, even if customers can’t use such high working conditions for the time being, they can reserve space for upgrading, avoiding the trouble of remodeling in the later stage.

    Extreme Environmental Conditions

    The extreme environment of steel mills determines that casting cranes must have a strong ability to adapt to the environment, and the components of ordinary cranes simply can not withstand this test.

    In terms of steel structure, high-temperature-resistant and fatigue-resistant high-strength steel must be used, and the main beam adopts a double-girder box structure to enhance the rigidity and resistance to deformation, and at the same time, a heat-resistant shield is added under the main beam to block the high temperature of the steel splash and slag erosion.

    The electrical system is the key object of protection. Motors, brakes, electrical control cabinets should be insulated, sealed to avoid high temperatures and dust into the cable using high-temperature resistant models, can be in a high-temperature environment for a long time to work stably; part of the large equipment will also be equipped with electrical cabinet air conditioning, reduce the internal temperature, to extend the service life of the electrical components.

    These special designs may seem to increase the cost of the equipment, but in fact it is to adapt to the extreme environment of the steel plant, reduce the later failure and maintenance costs, to ensure the long-term stable operation of the equipment.

    Key Technical Factors in Choosing a Casting Crane

    The core of choosing a Casting Crane is to match the actual operational requirements of the steel mill, and every technical parameter should not be sloppy. Many customers only look at the lifting capacity, ignoring other key factors, resulting in poor adaptability of the equipment, frequent failures. Combined with Henan Mine Crane’s project experience, the following technical factors must be focused on when selecting the type.

    Lifting Capacity and Configuration

    The choice of lifting capacity should never be based only on the weight of molten steel, which is the most common selection misunderstanding. The correct approach is that the weight of molten steel, ladle weight, spreader weight all counted, but also to leave a full 10% -20% of the safety margin, to avoid the equipment is in a state of full load for a long time.

    For example, lifting 40 tons of molten steel, ladle weight of about 12 tons, spreader weight of about 3 tons, then the rated lifting capacity of the crane should be at least 55 tons, in order to ensure safety. If there is a double package lifting, heavy-duty auxiliary material lifting needs, but also to appropriately increase the lifting capacity.

    Configuration, the mainstream casting cranes are used “main lift (lifting ladle) + secondary lift (equipment maintenance)” configuration, the main lift is responsible for the core of the molten metal transfer, the secondary lift is responsible for the maintenance of other equipment in the workshop, auxiliary materials lifting, to enhance the utilization of equipment.

    For large-scale steel mills, you can also choose double trolley and double hoist configuration, which can lift two ladles at the same time, or realize the rapid transfer of ladles to improve operational efficiency. Henan Mine Crane will customize the most suitable configuration according to the customer’s operation rhythm and demand, avoiding “too big for the job” or “too big for the job”.
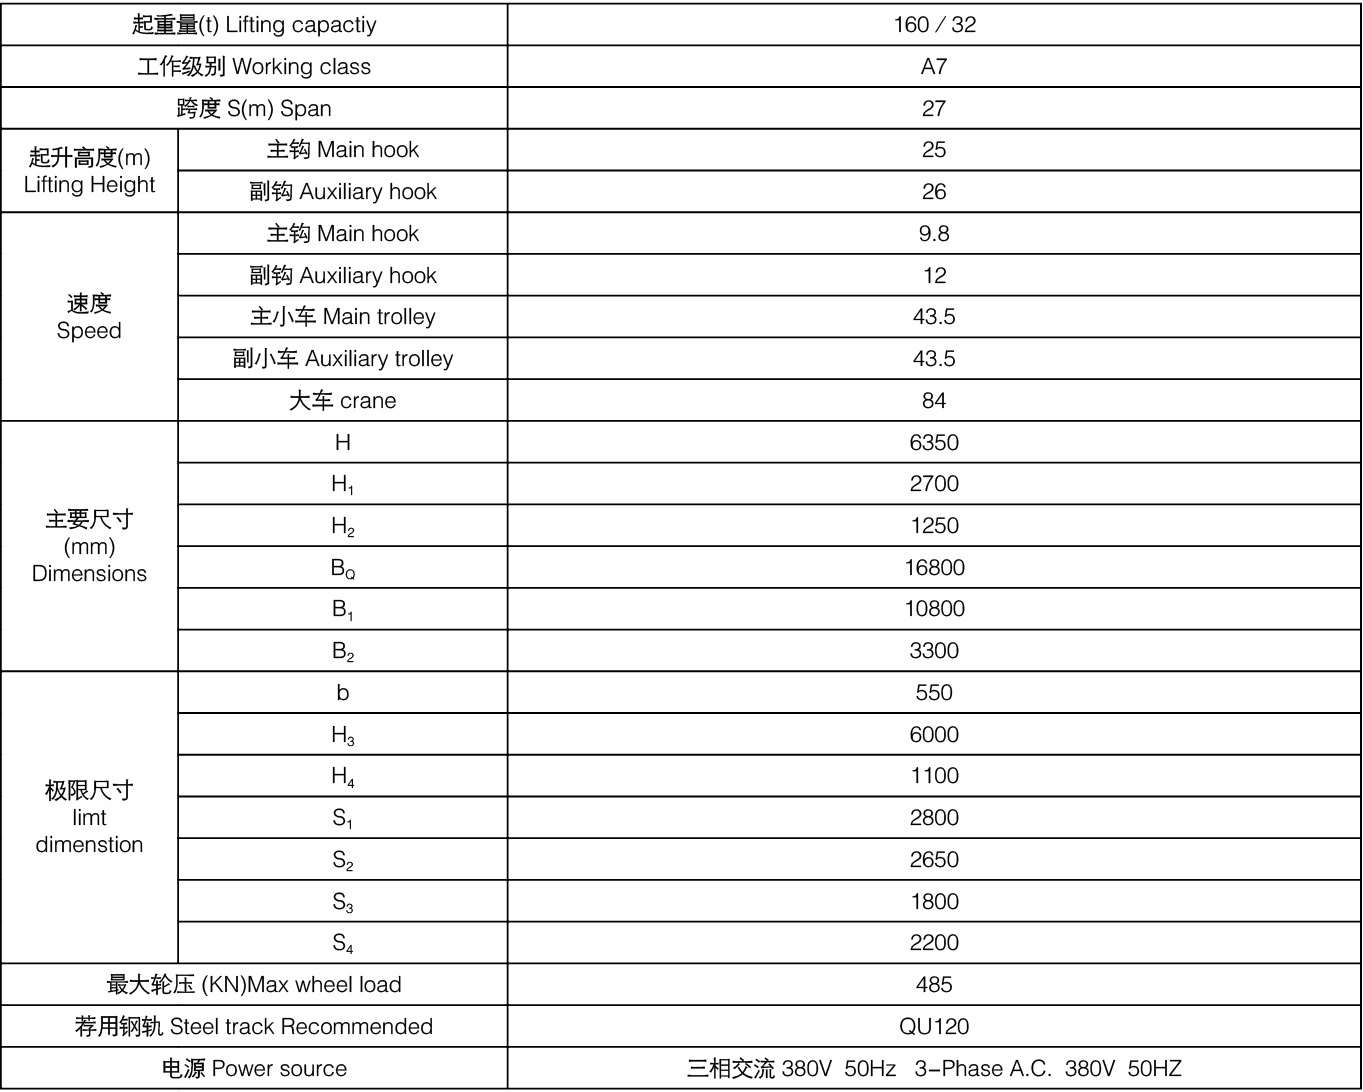
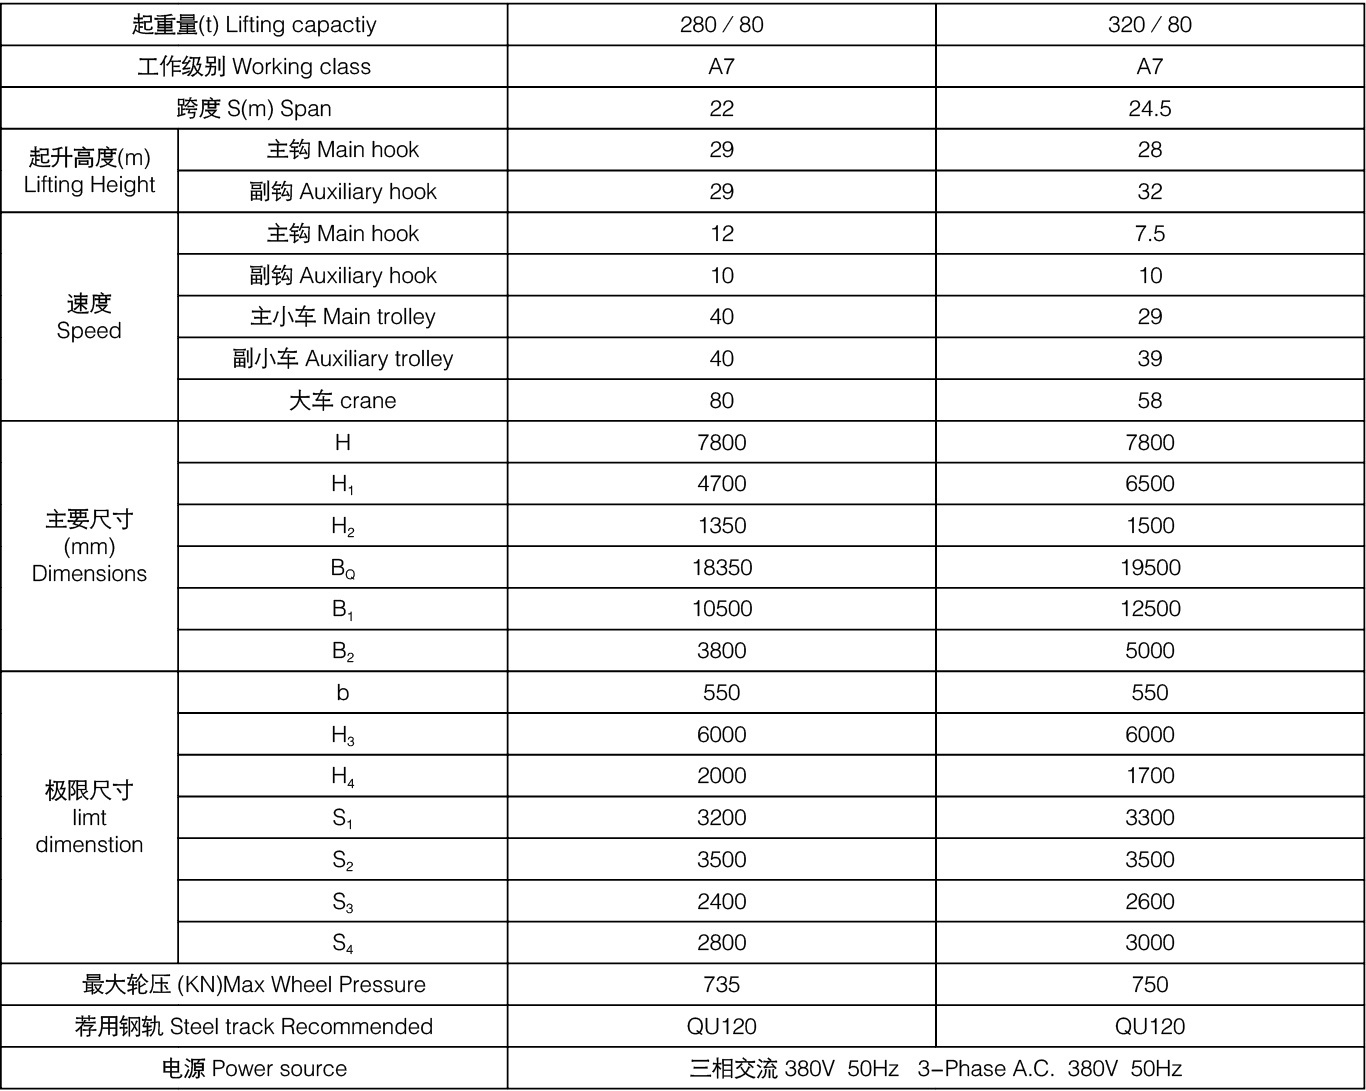
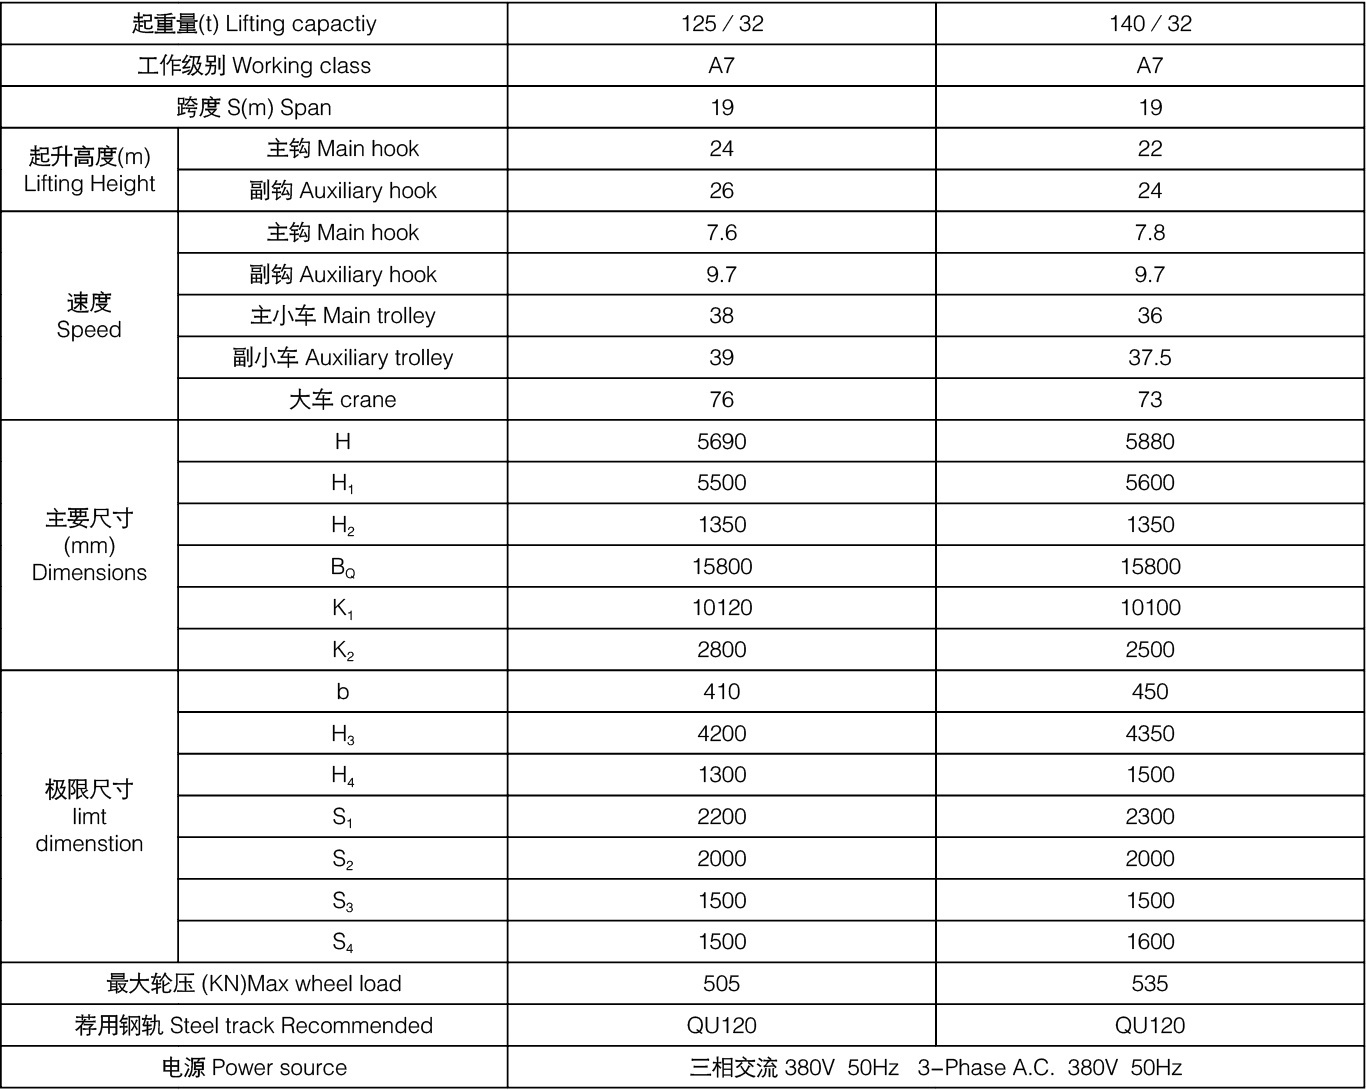
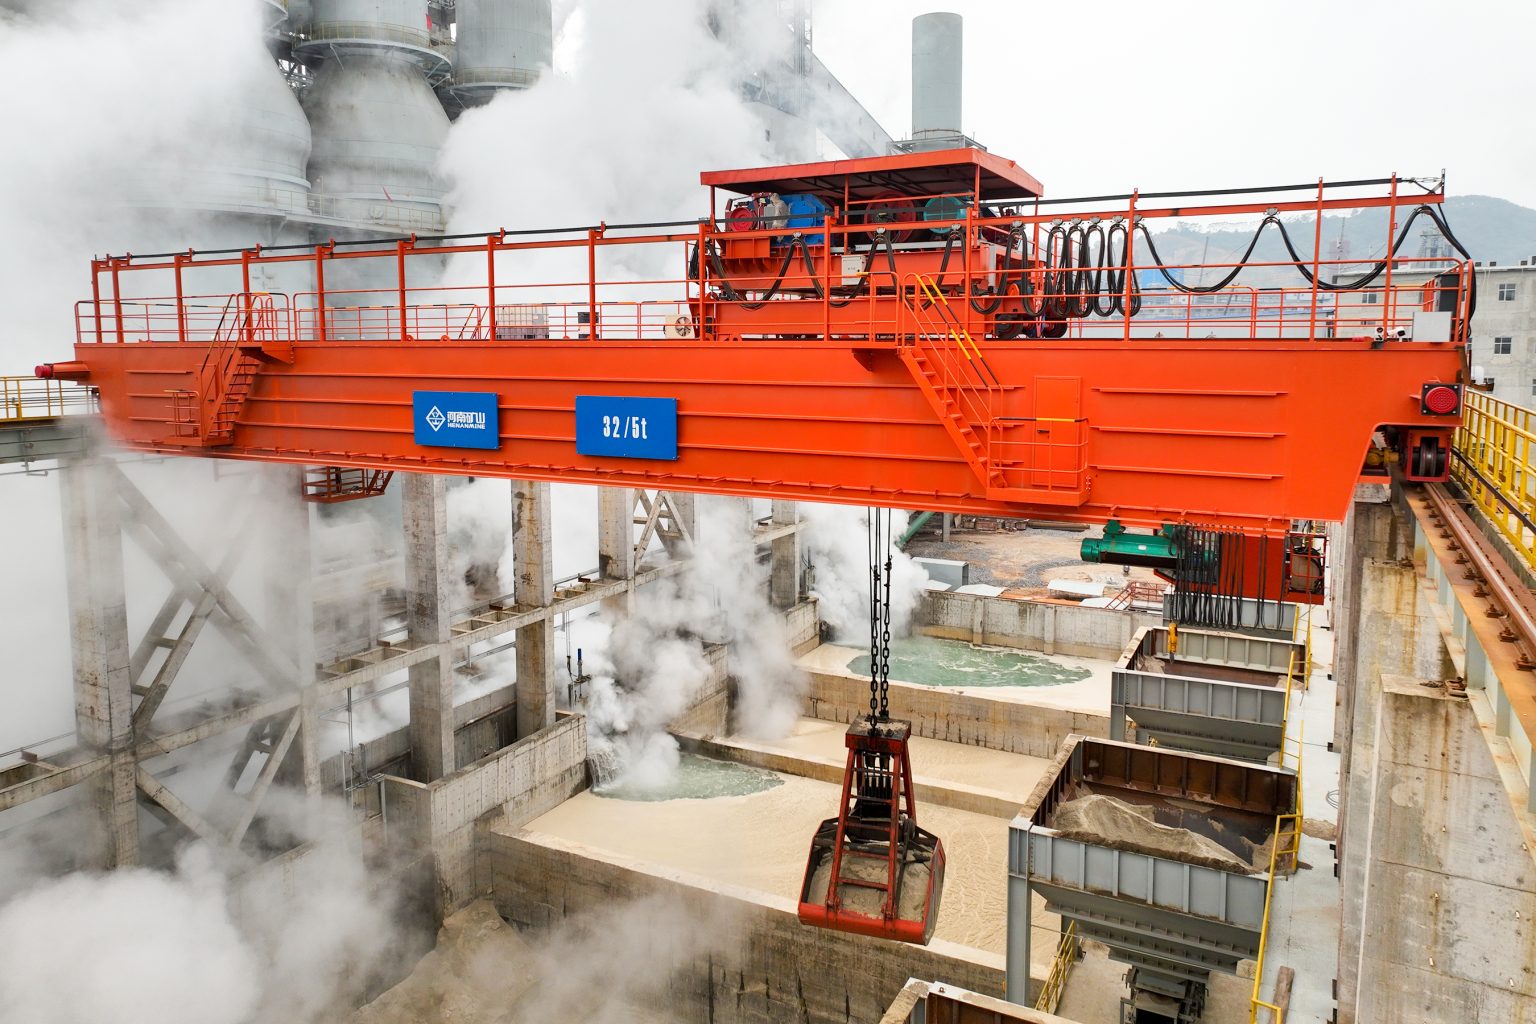
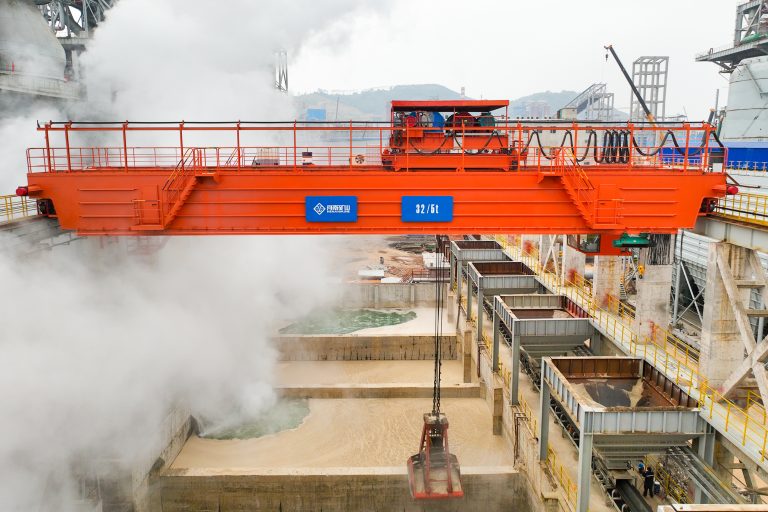
    Casting-Crane-Product-Specifications

    Duty Classification and Standards

    Duty Classification is the core parameter of casting crane selection, which directly determines the durability and service life of the equipment. As mentioned before, molten metal work must choose FEM A7-A8, ISO M7-M8, CMAA Class E-F equipment, which is the industry’s mandatory requirements, there can be no compromise.

    FEM A7 class: suitable for 10-20 lifts per day, medium load operations, such as small refineries, non-ferrous smelters, the equipment can withstand high-frequency starts and stops, but is not suitable for 24-hour continuous heavy loads.

    FEM A8 level: suitable for more than 20 lifting times per day, 24 hours continuous heavy load operation, such as large-scale converter workshop, continuous casting workshop, the structure of the equipment, the transmission system, the braking system have been strengthened, and can withstand high load operation for a long period of time, and the service life is longer.

    In addition, it is also necessary to ensure that the equipment meets the relevant industry standards, such as ISO 4301, GB/T 3811, etc., and the export project should also meet the local certification requirements to avoid problems in the later acceptance. Henan Mine Crane‘s casting cranes, all in line with international and domestic standards, according to customer demand to provide the appropriate certification documents.
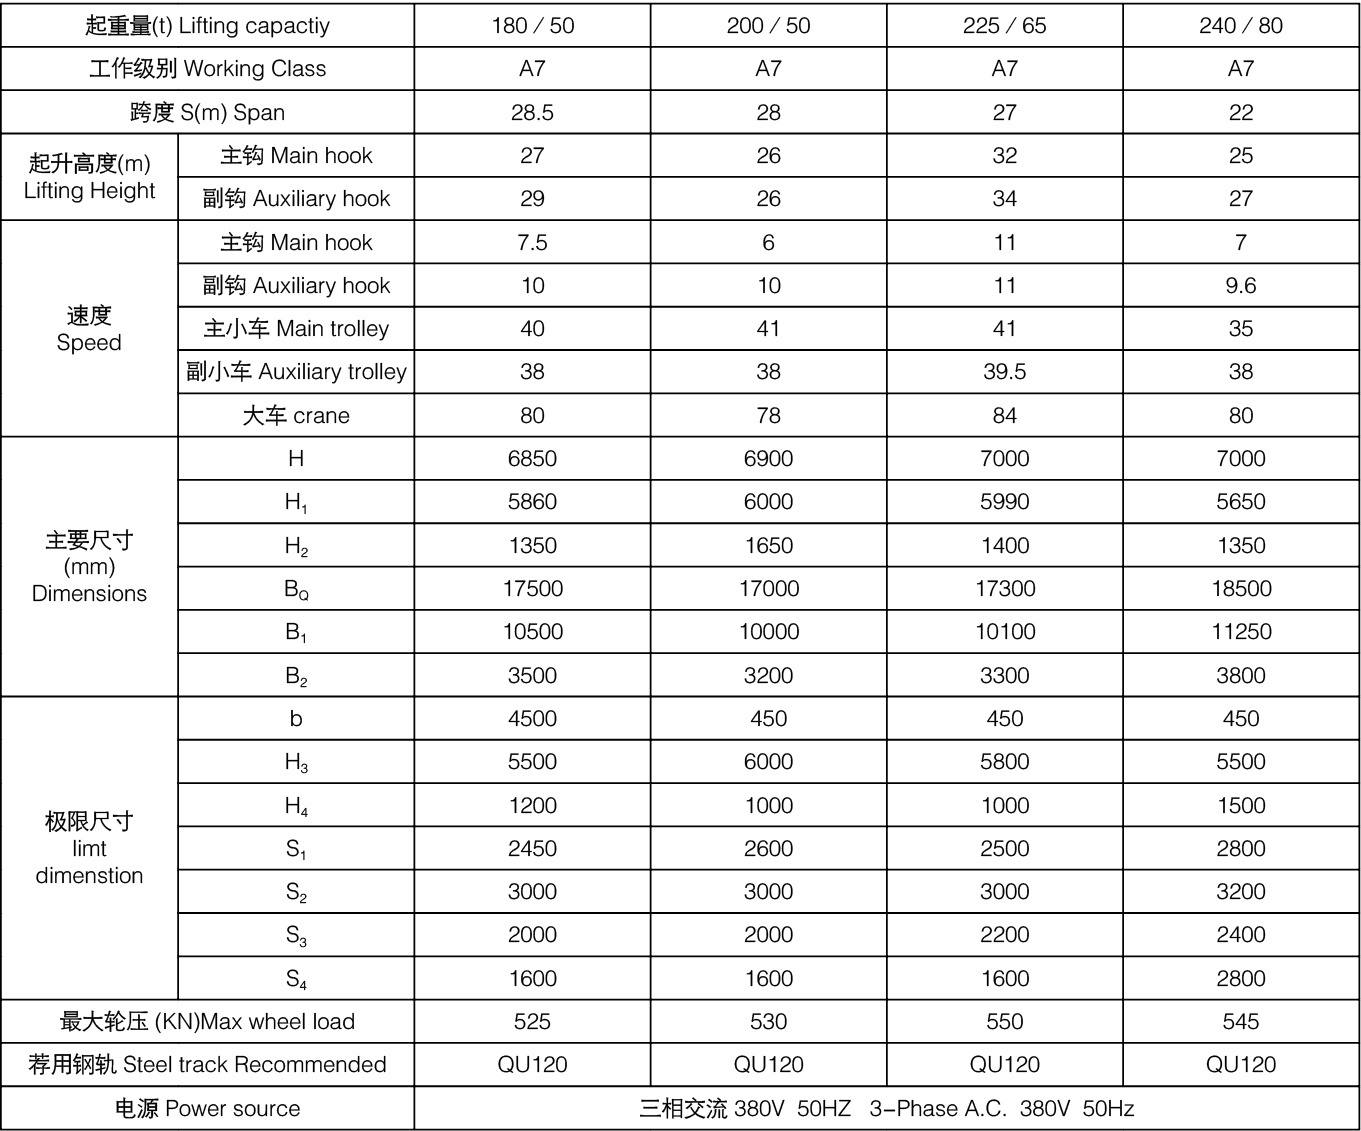
    Casting-Crane-Product-Specifications Casting-Crane-Product-Specifications Casting-Crane-Product-Specifications

    Structural Design Requirements

    Structural design of casting cranes, the core is “strong rigidity, resistance to deformation, high temperature”, double girder box structure is the standard, but also the core structural features of metallurgical overhead crane.

    The main beam of the double girder box structure is much more rigid than the single girder structure, which can effectively disperse the load pressure, reduce the shaking during the lifting process, and ensure that the steel is smooth to avoid spilling. The deflection of the main beam must be strictly controlled, usually not more than 1/1200 of the span, to ensure that the equipment will not appear obvious deformation even under full load.

    The material of the steel structure is also very critical, it must be made of high-strength steel of Q355B and above grade, and alloy steel is used in some key parts (e.g. outriggers, end beams) to enhance fatigue resistance and high temperature resistance. At the same time, the surface of the steel structure will do special anti-corrosion and heat-resistant treatment to extend the service life.

    Henan Mine Crane also optimizes the span of the main beam and the height of the outriggers according to the layout of the customer’s workshop to ensure that the equipment can be perfectly adapted to the workshop space, and to avoid interfering with the converter, continuous casting machine and other equipment.

    Hoisting System and Redundancy

    Hoisting system is the core of casting crane, directly related to the safety and stability of lifting, must have enough redundancy design, to eliminate single point of failure.

    The braking system must adopt double independent braking, a set of mechanical braking, a set of electromagnetic braking, both independent of each other, even if one set of failure, the other set of timely braking equipment to ensure that the ladle will not fall. The braking torque of the braking system must be more than 1.5 times of the rated load to ensure reliable braking.

    Lifting motor, gear box can also be configured according to the needs of redundant systems, such as dual motor, dual gear box, even if one of the set of failures, the equipment can continue to run, to avoid downtime affecting production.

    The wire rope and hook are the parts that directly carry the load and must have a very high safety factor. The steel wire rope is made of high-temperature-resistant and wear-resistant special steel wire rope with a safety coefficient of not less than 6 times; the hook is made of forged hook, equipped with anti-decoupling device to avoid the ladle from falling off, and meanwhile, regular flaw detection is carried out to ensure safety.
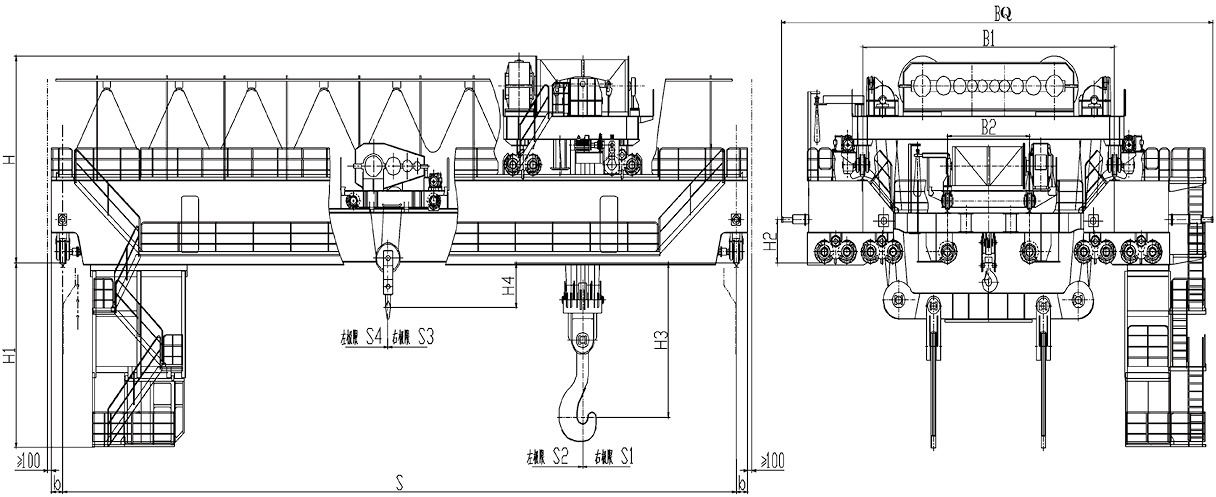
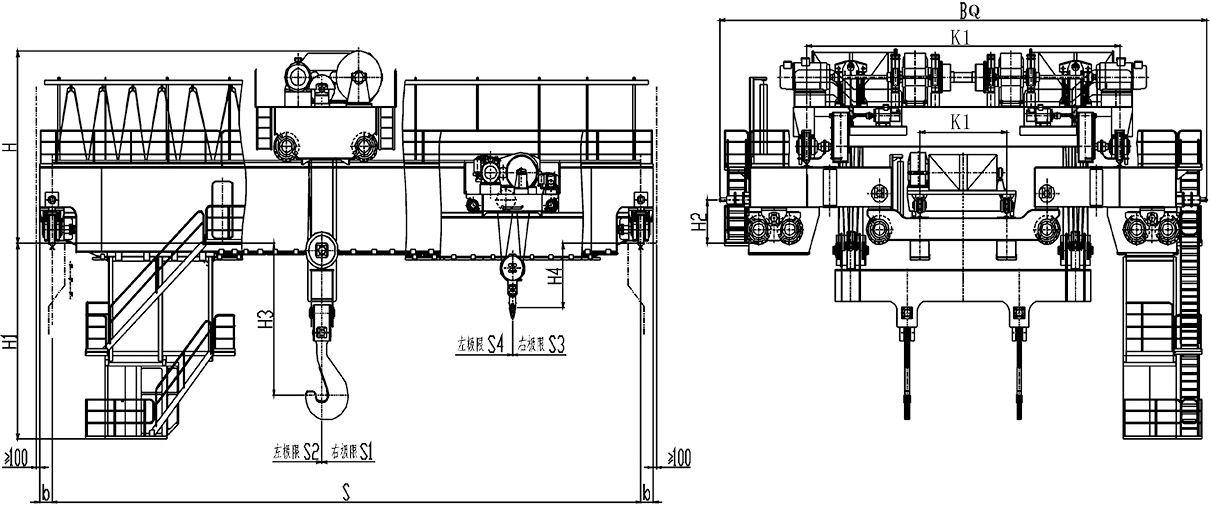
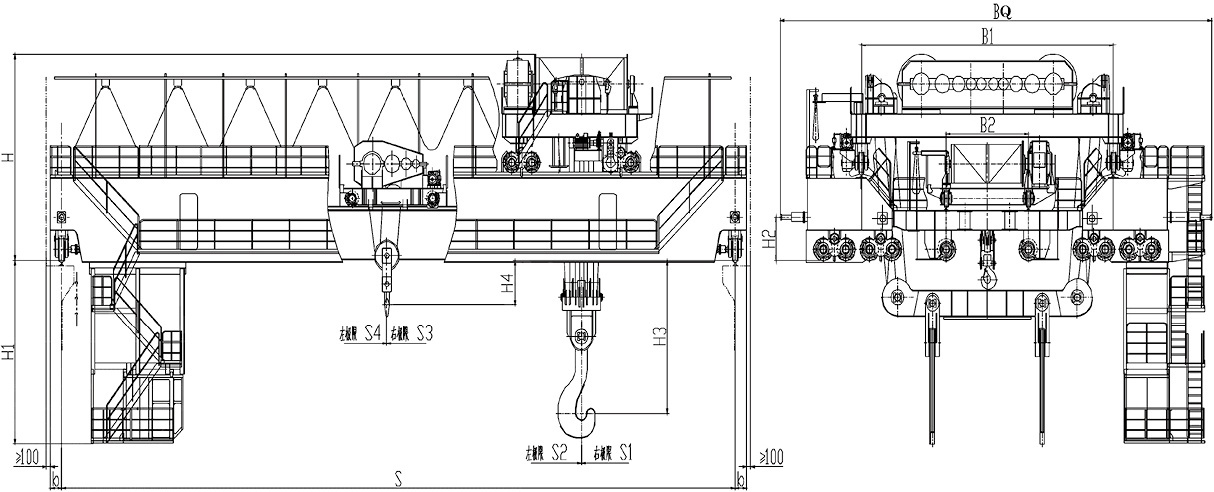
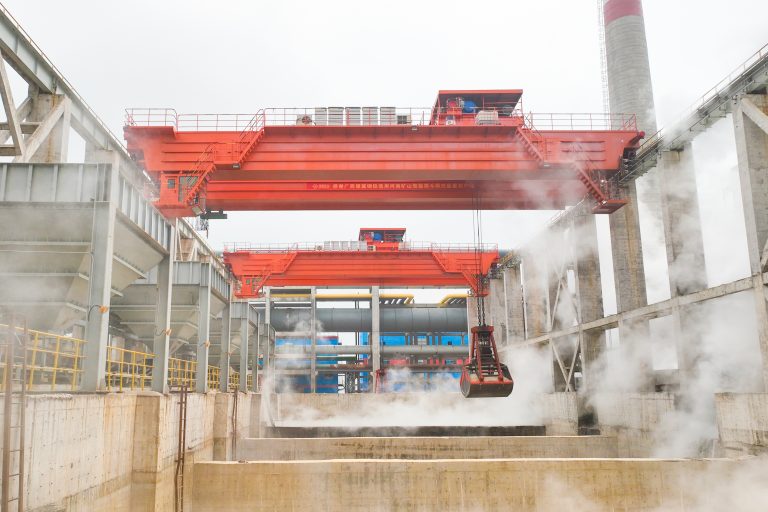
    Casting-Crane-Structure Casting-Crane-Structure Casting-Crane-Structure

    Heat Protection and Environmental Adaptation

    In view of the high temperature and dusty environment in steel mills, the heat protection design of casting cranes must be in place, which is also a key point of difference from ordinary cranes.

    Heat protection cover is installed under the main beam, which is made of high-temperature-resistant plate, can effectively block the high temperature of steel splashing and slag erosion, and protect the main beam, the electrical components and hoisting system underneath.

    The motor, brake and electrical control cabinet should be insulated, the shell is made of high temperature resistant material, and the internal heat dissipation device is added to avoid the aging and failure of the parts caused by high temperature. The electrical control cabinet can also be equipped with an air conditioning system to control the internal temperature in a suitable range to ensure the stable operation of electrical components.

    The cable is made of high temperature resistant cable, which can work stably for a long time under the high temperature environment of over 150℃, and at the same time, the cable is well protected to avoid being damaged by dust and slag. For workshops with serious dust and corrosive gases, the sealing performance of the equipment should be strengthened to prevent dust and corrosive gases from entering the equipment.

    Essential Safety Features for Molten Metal Handling

    Molten metal operation, safety is the first place, casting crane safety configuration, absolutely can not be saved.

    The following core safety features, is the selection must focus on, but also molten metal crane safety features of the core content.

    Mechanical Safety Systems

    Dual independent braking system is the most important, this is to protect the ladle safety of the last line of defense, must ensure that the two sets of braking system is independent of each other, do not affect each other, even if one of the set of failures, the other set can also work normally.

    Safety hooks must be equipped with anti-decoupling devices to prevent the ladle from falling off in the lifting process, while the hooks should be regularly flaw detection, cracks, wear and tear and other problems found, replaced immediately, can not be forced to use.

    The overload protection system should monitor the lifting load in real time, and once it exceeds the rated load, it will cut off the lifting power immediately and send out an alarm signal at the same time, so as to avoid overload operation of the equipment and prevent accidents such as deformation of the structure and breakage of the wire rope.

    In addition, it should be equipped with rope breakage protection, lifting height limit, running limit and other devices to ensure the safety of equipment operation in all aspects and eliminate any potential safety hazards.

    Electrical and Control Safety

    The electrical control system adopts PLC-based safety control system, which can realize precise control of the equipment, and at the same time has the function of fault diagnosis and alarm, once there is an electrical fault, it can send out an alarm signal in time, which is convenient for the staff to investigate and deal with it.

    Limit switches must be redundantly designed, with two sets of lifting height limit and running limit, to ensure that when one set fails, the other set can work normally, to avoid over-traveling of the equipment, which may cause collision, fall and other accidents.

    Emergency stop and safe descent functions are essential.

    Emergency stop button should be installed in the position easily accessible to the operator, such as the driver’s cab, ground operation station, in the event of an emergency, it can immediately cut off the power supply of the equipment and stop all the actions; safe descent function, in the event of power failure, brake failure and other emergencies, the ladle will be lowered smoothly to a safe position to avoid the expansion of the accident.

    Operational Safety Enhancements

    Anti-swaying control device can effectively reduce the swaying of ladle during lifting and transportation, especially during lifting, running and braking, it can control the swaying amplitude of ladle in the smallest range, avoiding the spillage of steel, and at the same time, improve the operational precision.

    For the workshop of multi-crane operation, it must be equipped with anti-collision system, which can monitor the running position of multiple cranes in real time, and once the risk of collision occurs, it will send out an alarm signal immediately and automatically slow down and stop, so as to avoid collision between cranes, which will damage the equipment and cause accidents.

    The cab should be insulated, dustproof treatment, equipped with air-conditioning system to improve the working environment of the operator; at the same time, the cab should have a wide field of vision to ensure that the operator can clearly observe the ladle and the operation area, to avoid operational errors. For high-temperature and high-risk areas, it can also be equipped with remote control function, so that the operator can operate the equipment in the center control room to reduce the risk of on-site operation.

    Casting Crane vs Standard Overhead Crane

    Comparison Factor Casting Crane Standard Overhead Crane
    Application Molten metal handling (molten steel, molten iron, non-ferrous metal melts) General material handling (steel, equipment, components, etc.)
    Duty Class FEM A7–A8, ISO M7–M8, CMAA E–F Typically A3–A5, suitable for low-frequency, light to medium-load operations
    Safety Redundancy Multiple redundant systems (dual brakes, dual limit switches, overload protection, etc.) with strong pertinence Standard safety configuration, no special redundant design
    Heat Protection Essential (heat-resistant shields, high-temperature components, heat insulation treatment) Usually not included, unable to withstand high-temperature environments
    Reliability Requirement Extremely high, requiring 24/7 continuous stable operation with zero fault tolerance Medium to high, suitable for regular operations, allowing occasional failures

    Simply put, the core of the design of ordinary overhead cranes is “to meet the ordinary material handling”, while the core of the design of casting cranes is “to deal with molten metal high-risk, high-load, high-temperature conditions. The use of ordinary overhead cranes to lift molten metal, like a family car to pull heavy cargo, not only easy to damage the equipment, but also buried serious safety hazards.

    Henan Mine Crane has encountered many customers, in order to save costs, with ordinary overhead cranes instead of casting cranes, and finally either because of frequent equipment failure downtime, or because of the safety hazards required by the regulatory authorities to rectify the situation, but instead of spending more money, the loss is not worth it.

    Automation and Smart Features in Modern Casting Cranes

    With the level of intelligence and automation in steel mills, casting cranes are also being upgraded, automation and smart features, not only to improve operational efficiency, but also reduce the number of operators on site, reduce operational risks, which is also the future development trend of metallurgical cranes.
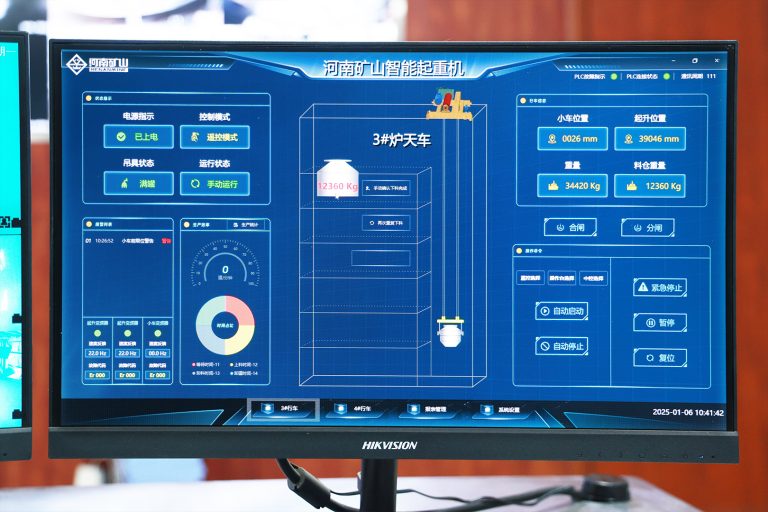
    Advanced Control Systems

    Modern casting cranes commonly use PLC and VFD (variable frequency) control systems, which can realize the smooth control of lifting and running, reduce the shaking of the ladle, and improve operational accuracy. Variable frequency control can also realize stepless speed regulation, avoiding the impact when starting and stopping, protecting equipment parts and prolonging service life.

    The anti-shaking control technology is also constantly upgraded, through the intelligent algorithm, it can adjust the lifting and running speed in real time, and control the shaking amplitude of the ladle in the smallest range, especially in the high lifting height and large span operation, the effect is more obvious, avoiding the spillage of steel, and guaranteeing the safety of operation.

    Remote and Automated Operation

    Remote control function allows the operator to operate the casting crane in the control room, without having to work in the high temperature and high risk workshop, which not only improves the working environment of the operator, but also reduces the risk of on-site operation.

    For large steel mills, automated workshops, can also realize the fully automatic operation of casting cranes, through the workshop with the MES / SCADA system docking, to realize the automatic issuance of operating instructions, automatic lifting of ladles, automatic monitoring of equipment status, the whole process without human intervention, significantly improve operational efficiency and reduce human error.

    Henan Mine Crane’s casting cranes can be customized according to the customer’s intelligent needs, remote control, fully automated operation of the program, to adapt to the intelligent transformation needs of different steel mills, to help customers achieve efficient, safe and intelligent production.

    Intelligent Monitoring and Predictive Maintenance

    Intelligent monitoring system can monitor the running status of the equipment in real time, including load, temperature, vibration, brake clearance and other parameters, and once abnormalities occur, an alarm signal will be sent out immediately, so as to facilitate timely investigation and treatment by the staff to avoid equipment operation with disease and reduce the breakdown and shutdown.

    Predictive maintenance technology, through the analysis of equipment operation data, can pre-judge the wear and tear of components, such as the service life of the wire rope, the degree of wear and tear of the braking system, and arrange for maintenance and replacement in advance, to avoid sudden failures and reduce downtime losses.

    At the same time, the equipment can be docked with the MES/SCADA system of the steel plant to realize the real-time uploading and sharing of equipment operation data, which is convenient for the managers to fully grasp the status of the equipment, formulate scientific maintenance plans, and improve the efficiency of equipment management.

    Key Considerations for Steel Plant Integration

    Casting cranes are not isolated equipment, and must be perfectly integrated with the production process and workshop layout of the steel plant, otherwise, even if the equipment itself is of good quality, it will not be able to maximize the role, and even affect the production efficiency. When selecting a model, these factors related to the integration of the steel plant must be considered.

    Workshop Layout and Crane Configuration

    First of all, the span, lifting height and hook limit distance of the crane should be determined in conjunction with the layout of the workshop. For example, the span of the converter workshop is usually determined according to the number of converters and the layout, usually between 30-40 meters; the lifting height should meet the needs of the ladle transfer from the converter to the refining furnace and continuous casting machine, and at the same time, it should also leave enough safety margin to avoid interference with the pipelines and structures on the top of the workshop.

    The limit distance of the hook is also very critical to ensure that the hook can smoothly transport the ladle to the designated location, such as the steel outlet of the converter, the entrance of the refining furnace, the continuous casting machine above the crystallizer, to avoid the dead angle of transportation.

    Henan Mine Crane’s engineers will come to your home to survey the workshop site and customize the appropriate crane span, lifting height and hook configuration to ensure that the equipment can be perfectly integrated into the production process and improve the operational efficiency, taking into account the customer’s production process and workshop layout.

    Power Supply and Reliability

    Casting cranes are heavy equipment with high requirements for power supply stability. Any interruption in power supply will not only affect production, but may also prevent the ladle from being lowered, leading to safety accidents.

    Therefore, steel mills must be equipped with a stable power supply system for casting cranes, it is recommended to use a double circuit power supply, once one of the circuits failures, the other circuit can be immediately switched to ensure that the equipment operates normally. At the same time, but also equipped with emergency power supply, in the case of sudden power failure, can provide temporary power supply for the equipment, the ladle will be smoothly lowered to a safe position to avoid the expansion of the accident.

    In addition, the stability of the power supply voltage is also very important, the voltage fluctuation should not exceed ±5%, otherwise it will affect the normal work of the electrical system, resulting in motor burnout, control system failure and other problems.

    Multi-Crane Coordination

    For large steel mills, a workshop may have more than one casting crane operating at the same time, which needs to consider the coordination of multiple cranes to avoid mutual interference and collision.

    First of all, we should be equipped with anti-collision system, real-time monitoring of the operating position of multiple cranes, once the risk of collision, immediately send out an alarm signal, and automatically slow down, stop, to ensure equipment safety. Secondly, it is necessary to reasonably divide the operating area, clarify the operating range of each crane, avoid cross operation, and improve operational efficiency.

    For scenes that require coordinated operation, such as double cranes jointly lifting heavy steel bales, but also equipped with synchronization control system to ensure that the two cranes are lifted, running at the same speed, to avoid tilting and shaking of the bales, to protect the safety of the operation.

    Maintenance Strategy for Casting Cranes

    The service life of casting cranes depends not only on the quality of the equipment itself, but also on the later maintenance. A set of scientific maintenance strategy can extend the service life of the equipment for 5-10 years, reduce the failure downtime rate, reduce maintenance costs. Combined with Henan Mine Crane’s experience, the following maintenance points must be focused on.

    Preventive Maintenance Planning

    Preventive maintenance is the core, can not wait for the equipment is broken and then repair, according to the intensity of the operation of the equipment and parts of the wear cycle, the development of regular maintenance program.

    Daily Maintenance: Before each day’s operation, check the braking system, wire ropes, hooks, limit switches and other key components to ensure that there is no abnormality; after the operation, clean up the dust and slag on the surface of the equipment, and check whether the electrical wiring is firm.

    Regular maintenance: carry out a weekly comprehensive inspection of the equipment, focusing on checking the lubrication of the gear box and motor, and replenish the lubricating oil; monthly check the brake clearance, wear and tear of the steel wire rope, adjust the braking system, and replace the parts with serious wear and tear; carry out an ultrasonic flaw detection on the steel structure once a year, to check whether there are any cracks, deformations and other problems, and repair them in a timely manner.

    Heat-Related Wear Management

    Under the high temperature environment, the parts of the equipment will wear out faster, especially the electrical parts, seals, wire ropes, etc., which must be paid attention to.

    Regularly check the heat insulation and sealing of electrical parts, and replace aged high temperature cables and seals; check the high temperature resistance of steel wire ropes, and replace them immediately when corrosion and broken wires are found; check the integrity of heat-resistant protective cover, and repair damaged parts in time to avoid high temperature erosion of equipment.

    At the same time, the dust inside the equipment should be cleaned up regularly to avoid the accumulation of dust leading to wear and tear of parts, electrical short circuit, and to prolong the service life of the equipment.

    Predictive Maintenance Technologies

    Predictive maintenance can be realized with the help of intelligent monitoring systems, which can effectively reduce sudden failures. By installing vibration sensors, temperature sensors and other equipment, we monitor the operating status of motors, gearboxes and braking systems in real time, analyze the operating data of the equipment, and anticipate the wear and tear of components in advance.

    For example, through the vibration sensor to monitor the vibration frequency of the gear box, once the vibration frequency is abnormal, it indicates that the gear box may be worn out, failure, and in advance to arrange for maintenance and replacement, to avoid gear box damage caused by equipment downtime.

    Spare Parts and Service Support

    Stockpiling necessary spare parts is the key to minimizing downtime losses. For fragile parts, such as wire rope, brake pads, seals, high temperature cables, etc., it is necessary to reserve enough safety stock, so that once the parts are damaged, they can be replaced in time to avoid long downtime.

    Choose a strong and experienced supplier to get more professional after-sales support. Henan Mine Crane provides each customer with an exclusive after-sales team, which makes regular visits to solve problems encountered in the process of equipment maintenance; at the same time, it provides sufficient supply of spare parts to ensure that when the equipment fails, it can be quickly responded to and repaired in a timely manner.

    Common Mistakes When Choosing a Casting Crane

    Combined with more than twenty years of industry experience, I summarized the most common 5 misconceptions when choosing a casting crane, many customers have stepped on these pits, I hope you can avoid.

    The first pit, using ordinary overhead cranes instead of casting cranes. This is the most dangerous and common misunderstanding, ordinary cranes do not have high temperature resistance, redundant safety systems, can not withstand the high risk of molten metal operations, it is easy to cause safety accidents, and the maintenance costs of the later period will also increase significantly.

    The second pit, underestimate the working level requirements. Many customers only look at the lifting capacity, ignoring the level of work, selected a low level of equipment, resulting in frequent equipment failures, the service life is greatly shortened. For example, 24-hour continuous operation of the converter shop, you must choose FEM A8 level, choose A7 level will be overloaded, wear and tear too fast.

    The third pit, ignoring redundant safety systems. Some customers in order to save costs, omit the double braking, redundant limit and other safety configurations, it seems to save money, but actually buried a serious security risks, once the failure, the consequences are unimaginable.

    The fourth pit, overlooking heat protection and environmental factors, especially small and medium-sized steel mills, it is easy to ignore the high temperature, dust on the impact of the equipment, selected no heat protection, sealing performance is poor equipment, resulting in rapid aging of the equipment components, frequent failures, maintenance costs remain high.

    The fifth pit, choose a supplier without metallurgical crane experience. The design, production and installation of casting cranes require rich experience in the metallurgical industry, many suppliers do not have relevant project experience, the production of equipment can not be adapted to the working conditions of the steel plant, and it is easy to appear in the late stage of various problems, after-sales can not be followed up in a timely manner.

    Henan Mine Crane has been focusing on heavy metallurgical cranes for more than twenty years, and has participated in many large-scale steel plant projects at home and abroad, and has accumulated rich experience, which can help you avoid these misunderstandings and select the appropriate equipment.

    Casting Crane Selection Checklist

    In order to facilitate you in the procurement inquiry (RFQ), clear their own needs, to avoid deviation in the later stage, I have compiled a casting crane selection checklist, fill in against, you can clearly sort out their own purchasing needs, but also allows the supplier to more accurately for you to quote.

    1. Rated lifting capacity (need to include the weight of the ladle, spreader, reserve 10% -20% safety margin)
    2. Crane span, lifting height, hook limit distance
    3. Working class requirements (FEM/ISO/CMAA, minimum A7 recommended)
    4. Safety redundancy requirements (whether dual brakes, dual motors, redundant limits, etc. are required)
    5. Operating environment parameters (maximum ambient temperature, dust concentration, corrosive gas conditions)
    6. Automation and control requirements (whether remote control, fully automatic operation, anti-shaking control are required)
    7. Applicable standards and certification requirements (domestic GB standards, international ISO standards, export projects need to comply with local certification)
    8. Installation and commissioning requirements (whether the supplier needs to install and commission at home)
    9. After-sales and spare parts support (whether to provide regular inspection, spare parts supply)

    Frequently Asked Questions

    Q1: What is the difference between a casting crane and a ladle crane?

    Actually there is no difference between the two in essence, they are both cranes specially designed for lifting molten metal ladles, just called differently. Casting crane is a common name, ladle crane (ladle crane) is more focused on the “lifting ladle” call, Henan Mine Crane production of such cranes, no matter what kind of name, the core performance and safety standards are the same, can meet the needs of molten metal handling.

    Q2: What duty class is required for molten metal handling?

    Molten metal handling requires a very high duty class for cranes, usually FEM A7-A8, ISO M7-M8, or CMAA Class E-F. The specific duty class you choose depends on your needs. Which class to choose depends on the intensity of your work: if it is high frequency, 24 hours continuous work (such as large converter shop), choose FEM A8 class; if it is medium frequency, medium load work (such as small refinery), choose FEM A7 class can be.

    Q3: Why are dual brakes required for casting cranes?

    Because molten metal operations are extremely risky and a falling ladle can cause a catastrophic accident if the braking system fails. Dual braking system (mechanical brake + electromagnetic brake) ensures that when one set of brakes fails, the other set can stop the equipment in time, locking the ladle firmly and avoiding accidents, which is a mandatory safety requirement for molten metal operation and the core of molten metal crane safety features.

    Q4: Can casting cranes be automated?

    Yes, you can. Modern casting cranes fully support automation and remote control, through PLC, frequency control system, and docking with the MES/SCADA system of steel mills, they can realize fully automated operation – automatic reception of operating instructions, automatic lifting of ladles, automatic monitoring of the status of the equipment, the whole process without human intervention. Henan Mine Crane can customize the automation solution according to your intelligent needs to improve the operation efficiency and reduce the operation risk.

    Q5: What is the typical lifespan of a casting crane?

    Under the premise of reasonable design and standardized maintenance, the service life of a casting crane can usually reach 20-30 years or even longer. Henan Mine Crane’s casting cranes are made of high-strength steel, high-quality components, coupled with scientific structural design, as long as the regular maintenance is done, they can operate stably for a long time, saving the cost of equipment replacement for the steel mills.
    Conclusion

    Casting cranes, steel mills, metallurgical plants molten metal operations, “lifeline”, its selection, directly related to production safety, operational efficiency and long-term operating costs.

    Selection of casting cranes, can not only look at the price, look at the lifting capacity, but also pay more attention to the level of work, safety redundancy, heat protection and steel plant integration adaptability. They are not ordinary lifting equipment, but specialized equipment tailored for high-risk, high-load, high-temperature working conditions, where every design is about safety and durability.

    Henan Mine Crane Factory Custom

    Henan Mine Crane has been focusing on the design, production and service of heavy metallurgical cranes for more than 20 years, witnessing the development of countless steel mills and accumulating rich experience in selection and operation. We always adhere to the principle of “safety first, fit first”, from site survey, program design to installation and commissioning, after-sales support, to provide you with professional services, to help you choose a truly suitable casting crane, to avoid selection errors, to protect production safety and efficiency.

    Choosing a suitable casting crane is not only a purchase investment, but also an investment in the production safety and long-term development of the steel mill. Only choose the right equipment, do a good job of maintenance, in order to make it become a steel production “right-hand man”, for you to create greater value.
    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose a Carbon Block Stacking Crane for Chemical Plants?

    How to Choose a Carbon Block Stacking Crane for Chemical Plants?

    How to Choose a Carbon Block Stacking Crane for Chemical Plants?

    The wrong crane is selected for carbon block warehouse, which not only affects production capacity, but also hides safety risks.Dust, combustible gas and corrosive medium coexist in chemical and carbon products workshops. Heavy carbon blocks need to be handled frequently and accurately during operation. Ordinary cranes are easy to induce fire accidents.

    Carbon block special stacking crane is specially designed for this harsh working condition, suitable for carbon processing, aluminum electrolysis, chemical scene, can safely complete carbon block grab, transfer and stacking.The core of the selection is not tonnage, but matching the fixture, automation system and explosion-proof and anti-corrosion protection configuration according to the field conditions.

    This article will disassemble the core selection standards in detail, assist enterprises to select safe, stable and adaptable carbon block stacking cranes, and ensure efficient, compliant and controllable operation in the factory area.

    What Is a Carbon Block Stacking Crane?

    Carbon block stacking crane is a special bridge crane, cancel the traditional hook and ordinary grab, equipped with exclusive clamping tooling.The equipment can vertically clamp the whole row of carbon blocks (conventional 19 blocks, 21 blocks) at one time, and complete the whole process of carbon block production, baking, cooling and storage as a unit. The operation efficiency is much higher than that of ordinary lifting equipment for single block lifting.

    The core components of the equipment are as follows:

    1. Bridge structure: the overall welded box beam structure, strong rigidity, anti-fatigue, anti-deformation, long-term adaptation to high-frequency, heavy-duty continuous reciprocating operation, stable operation without shaking, equipment longer service life.
    2. Trolley travel mechanism: integrated high-precision drive and buffer structure, support the longitudinal movement of the whole machine track, lateral movement of the trolley bridge, stable start-stop without impact, accurate positioning, can cover the operation area in all directions, and ensure that the carbon block is transported without deviation and dislocation.
    3. Lifting mechanism: equipped with heavy-duty lifting and braking system, can accurately adjust the lifting speed, to achieve stable lifting of carbon blocks, slow drop, effectively avoid collision damage.At the same time, it has overload protection and power-off braking functions, which is safe and reliable, suitable for full-process material taking and stacking operations.
    4. Clamping device: customized tooling for the core of the equipment, optimized design according to the size and arrangement characteristics of the whole row of carbon blocks, uniform clamping force and firm attachment, which can effectively prevent the carbon blocks from loosening, deviation and sliding during the transfer process and ensure the materials are intact.
    5. Guidance system: equipped with high-precision positioning and guidance components, the load operation attitude is corrected in the whole process, the displacement error caused by equipment vibration and track deviation is offset, and the carbon block is transported vertically and stably, and the alignment is accurate, so as to meet the requirements of high-precision stacking conditions.
    6. Control system: PLC+VFD frequency conversion drive +HMI touch intelligent control system, which can realize intelligent operation such as accurate positioning, weight verification, automatic stacking, etc., support accurate control of the whole process of equipment, with safety functions such as fault self-test and overload protection, easy to operate and strong stability.

    Different from the general overhead crane, all structural parts of the equipment are customized and developed according to the weight, shape and precision handling requirements of carbon blocks, and are specifically adapted to special working conditions such as carbon products, aluminum electrolysis and chemical industry. Standard general cranes cannot meet the requirements of such special operations.

    Where These Cranes Are Used

    Carbon block stacking crane is widely used in the whole process of carbon products and aluminum production, covering multiple core operation sections, which can complete accurate and repetitive material handling operations under high-risk conditions. The main application scenarios are as follows:

    • Raw anode workshop:responsible for transferring the unbaked carbon blocks to the roasting furnace to ensure smooth connection of procedures;
    • Anode baking work area: complete raw carbon block loading into ring furnace and tunnel furnace, and accurately remove and transport the finished carbon block after high temperature baking;
    • Cooling and storage area: orderly stacking of roasted high temperature carbon blocks, support multi-layer three-dimensional storage stacking, and ensure the stability of materials without damage when the carbon blocks are cooled to the operating temperature;
    • Carbon block warehouse: coordinate the orderly stacking and inventory management of finished carbon blocks, and provide stable material supply for subsequent anode assembly processes;
    • Chemical and petrochemical plants: It is suitable for standardized and repetitive handling operations of various carbon-based materials, electrodes and bulk solid materials, and can perfectly adapt to the flammable, explosive and corrosive high-risk operating environment of the plant.

    If the plant involves multiple production sections at the same time, it is necessary to focus on verifying the adaptability of equipment: due to the differences in risk levels and working conditions of each section, it is necessary to evaluate whether the crane with uniform specifications can be compatible with multi-area operations, or configure customized equipment for different sections, so as to ensure operation safety and equipment operation stability.

    Key Selection Criteria: Load and Stacking Capacity

    Capacity planning for a carbon block stacking crane isn’t just about tonnage, it’s about matching the crane to your block dimensions, batch size, and stacking pattern.

    Block group size

    The most popular cranes are configured to pick up a batch of 19 or 21 blocks per cycle, stacked lengthways in the gripper. Check your block dimensions, batch size before specifying as the gripper beam length and pitch spacing is based on this number.

    Rated capacity

    On a crane, a typical 15–30 ton capacity is found for most sizes of block, with a larger installation having a higher rating. However, making the capacity too small because of previous capital, car, wiring and structure savings is one of the most common and costly selection errors,  as it constrains batch size and throughput permanently.

    Stacking height

    Specify the number of layers necessary with your storage scheme (multi-layer stacking which is usually up to 6-9 layers). The control system needs more accurate positioning as multi-layer stacking (which would exceed 6-9 layers) is more vulnerable to dislocation.

    Span and duty class

    Span should be the same width of your warehouse or workshop bay and duty class (typically A7 or 8) should be set for the amount the crane will continually run. If you set the duty for intermittent duty a crane would last only a very short time under 24/7 stacking.

    Gripper and Clamping System Design

    The clamping fixture is the single most application-specific part of a carbon block stacking crane, and it deserves more scrutiny than most buyers give it.

    • Mechanical v. hydraulic clamps.Mechanical grippers use a four-link gravity self-locking arrangement, allowing them to open and close without power and retain force with power lost mid-cycle. Hydraulic clamps employ proportional valve control,  to provide a variable clamp force to match block size and fragility, but require a hydraulic system to still retain force
    • Variable pitch.Seek grippers with a variable spacing (typically around +/-50 mm) so the same crane can lift blocks that vary marginally in size without a change of fixture.
    • Overload and leak protection.Weighing modules monitors clamped weight before lift and use automatic detection of fixture leakage and slip. No dropped loads! A potential disaster,when blocks of hundreds of kilos are stacked several meters high.
    • Wear life and serviceability. Find out from suppliers about the rated cycle life of gripper liners, and if individual grippers are removable and replaceable rather than if the entire fixture beam has to come down every time a gripper wears out.
    • High-temperature operation.Should the crane be expected to pull blocks from a baking furnace it will require heat resistant materials, and some form of insulation, as a generic Clamp would be doomed to failure.

    Explosion-Proof and Hazardous Zone Requirements

    The vast majority of carbon block equipment product data will ignore a core selection criteria, and for the chemical process area, rather than pure storage area of the crane, this point is crucial, that is, explosion-proof grade matching.

    Combustible gas, solvent vapor and carbon dust exist in carbon processing and chemical workshops. Electric parts of ordinary cranes are easy to produce sparks and have hidden dangers of explosion.Therefore, high-risk areas should be zoned according to ATEX and IECEx standards, and the crane electrical system must match the corresponding explosion-proof level to ensure safe operation.

    Practical steps for this section of your selection process:

    • Classify the zone first: It is necessary to cooperate with the plant safety engineer to accurately determine the risk type of the crane operation area, and identify whether it belongs to gas hazard, dust hazard or solvent vapor hazard scenario.The explosion-proof design scheme corresponding to different dangerous working conditions is completely different and cannot be applied universally.
    • Match the Ex-rating to the gas or dust group: Ex d IIB T4, Ex d IIC T4 and other explosion protection classes correspond to specific gas groups and ignitiontemperature Blindly high explosion-proof specifications will cause budget waste, while insufficient explosion-proof grades will leave major safety hazards, and accurate adaptation of working conditions and grades must be achieved.
    • Seal every electrical interface: In high-risk gas explosion-proof areas, all electrical enclosures and cable access ports of the crane must be completely sealed to prevent flammable gases from penetrating into the equipment and contacting electrical components, so as to avoid explosion risks from the source.
    • Don’t assume higher explosion-proof class is always better: The core of explosion-proof selection is to fit the officially approved regional grade of the factory, and the higher the grade, the better.Excessive high allocation will not only increase the equipment procurement cost for no reason, but also increase the difficulty of equipment overhaul and maintenance, and cannot bring actual safety gain.
    • Confirm compliance documentation: The explosion-proof performance of equipment shall not be based only on the oral instructions of the manufacturer, but must be certified by a third-party authority.Especially imported equipment, it is necessary to ensure that its explosion-proof qualification meets the local safety specifications for high-risk areas, and ensure that the equipment is put into use legally and in compliance with regulations.

    Corrosion and High-Temperature Resistance

    In addition to the risk of fire ignition in the chemical plant environment, various chemical media erosion will also cause significant equipment loss.The joint action of acid and alkali steam, high humidity air and carbon powder dust in the workshop will make the corrosion rate of ordinary steel and electrical shell much higher than that of conventional industrial plants.

    The following core protection schemes shall be clearly implemented for equipment selection:

    • The steel structure and exposed mechanical parts of the factory building shall be sprayed with anti-corrosive coatings or made of corrosion-resistant materials to withstand the erosion of acid and alkali steam, humid air and carbon powder to prevent corrosion of components and attenuation of structural strength.
    • Electrical equipment shall be sealed shell, in addition to meeting the standard explosion-proof grade, but also need to adapt to the special conditions of dust, high humidity and strong corrosion on site, so as to prevent medium intrusion and avoid various electrical faults.
    • Lifting accessories suitable for baking process shall be made of high-quality materials with high temperature resistance and thermal aging resistance, so as to effectively avoid deformation, loosening and failure of accessories under high temperature environment and ensure safe and stable lifting operation.
    • Equipment wearing parts selection needs to take into account mechanical wear and chemical corrosion double loss, chemical corrosion conditions will greatly reduce the service life of conventional parts, need to choose wear-resistant, corrosion-resistant composite special materials.

    When purchasing carbon block stacking cranes, confirm whether the equipment is optimized for chemical corrosion conditions.If there is no difference in material, structure, and protection between the ordinary model and the chemical version, it means that the equipment is not suitable and there are safety hazards, and should not be selected.

    Automation and Control Systems

    Modern carbon block stacking cranes range from fully manual cabin-operated units to fully automated systems that run entire stacking sequences without an operator in the loop.

    Control architecture. Look out for a PLC+VFD+HMI configuration. The combination gives repeatable precise positioning and real-time viewing of the operation through a point-n-click touchscreen. This configuration also facilitates remote recording of cycle counts and fault diagnostics.

    Operating modes. The majority of installations will ease operation by having at least one of:  cabin operation, remote radio control or dual-mode switching. (Dual-mode switching necessary for remote station operation or comfort of operation during maintenance/commissioning.)

    Positioning and weight verification. Most commercial systems employ a vertical position sensor and a weighing module: the crane is lowered to an programmable position, the clamp is applied after a “loose rope” condition is detected,  and then weight is confirmed before the lift is terminated. This safeguards against misalignments and overloads.

    Level of automation. Determine as early as possible if a fully automated system (grip,  place,  destack, and load the truck without operator intervention) is best,  or a semi-automated system where the operator loads or destacks from the semi and trucks, but the system does the handling.  Fully automated systems minimize labor and reduce operators’ time in the hazard zone but rely on tighter tolerances in your dimensions and storage layout to operate reliably.

    Structural and Mechanical Reliability

    Carbon block stacking crane core structure and transmission system, the core requirement is to adapt to long-term continuous heavy duty cycle operation, rather than only meet short-term peak load, the key configuration standards are as follows:

    1. Bridge structure: box beam integral structure, compared with traditional open truss structure, bending resistance, torsion resistance, deformation resistance is stronger, can perfectly adapt to the workshop high-frequency, uninterrupted heavy-duty reciprocating operation, long-term operation is not easy to deform, higher stability, adapt to high-intensity continuous production conditions.
    2. Walking drive mechanism: long-span models are equipped with double-drive walking structure, which effectively solves the problems of unstable single-drive operation, large vehicle deviation, track deviation, etc., greatly improves the stability and positioning accuracy of the whole machine operation, and ensures accurate and error-free carbon block transfer and stacking operations.
    3. Hoisting brake system: the main hoisting mechanism is equipped with double brake redundancy protection, which subverts the single brake structure of ordinary cranes.It can completely avoid the safety risks such as falling and damage caused by single brake failure and suspended load, and ensure the safety of heavy lifting operation from the hardware level.
    4. Equipment working level:equipment working level shall match the actual operation frequency on site, and A7/A8 high working level shall be selected for general use.It is strictly prohibited to refer to the rated tonnage parameters only in the selection, and it is necessary to match the working condition grade in combination with the continuous operation intensity of the workshop, so as to avoid overload fatigue operation of the equipment, ensure the long-term stable service of the equipment, and prolong the service life of the whole machine.

    Safety Standards and Certifications

    Carbon block stacking crane high-risk operating conditions, in addition to basic explosion-proof certification, but also to meet a full set of safety compliance standards, core requirements are classified as follows:

    1. Industry specifications and qualification documents: The equipment must strictly comply with the safety standards for overhead cranes in the project territory, and be equipped with complete official qualification materials such as equipment working level certificates and rated load test reports to ensure that the equipment parameters and performance meet the production compliance requirements of the factory.
    2. Hardware safety protection configuration: The lifting system is equipped with multiple limit protection devices, including upper and lower travel limit, over-travel forced protection and other functions, which can effectively eliminate safety accidents such as equipment collision and carbon block falling caused by over-winding and over-release, and build up hardware safety defense lines.
    3. Acceptance criteria for commissioning: Before the equipment is officially put into operation, it must pass comprehensive inspection, commissioning and acceptance by an authoritative third-party organization, issue a compliance acceptance report, and prevent the equipment from being put into use with hidden dangers and non-compliance.
    4. Procurement compliance principle: all safety, explosion-proof and detection-related qualification documents shall be verified and confirmed in advance at the procurement signing stage.It is strictly prohibited to supplement the compliance data after equipment installation, which can effectively avoid the high cost and shutdown risk caused by later rectification and transformation.

    Cost Factors and Total Cost of Ownership

    Carbon block stacking crane selection can not only pay attention to the purchase unit price, but also comprehensively consider the full life cycle use cost. The cost factors are classified as follows:

    1. Cost difference of equipment working condition level: low-cost and low-level equipment cannot adapt to long-term full-load continuous production, long-term high-intensity operation is easy to rapidly age, frequent failures, frequent overhaul or even replacement of the whole machine, short-term purchase advantages will be offset by high operation and maintenance and replacement costs in the later period, and the comprehensive cost performance is extremely low.
    2. Wear parts and maintenance costs: preferred to support more than 50,000 cycles of fixture wear bushing, with quick-change tooling structure, can greatly shorten the equipment maintenance, replacement of parts downtime, effectively reduce the equipment full-cycle operation and maintenance costs, ensure production continuity.
    3. Explosion-proof and anti-corrosion configuration hidden value: Although explosion-proof and anti-corrosion special accessories will increase the initial purchase investment of equipment, they can adapt to high-risk corrosion, flammable and explosive conditions, effectively avoid high hidden losses such as equipment failure, safety accidents, shutdown rectification and compliance penalties, and are safer and more economical for long-term use.
    4. Automation investment and labor cost: High automation configuration can greatly reduce the labor cost of single stacking and transfer, improve operation efficiency, but it will increase the initial cost of equipment, and it needs regular maintenance of supporting professional sensors and control systems, which is suitable for large-scale and high-frequency production scenarios.
    5. Spare parts supply chain downtime cost: focus on checking the supplier’s core wearing parts stock reserve and delivery cycle.Carbon block stacking crane is the core equipment of storage. Once the equipment is shut down due to shortage of accessories, the whole carbon block warehouse will be shut down directly, resulting in huge capacity loss.

    Choosing a Supplier

    Carbon block stacking crane is a special lifting equipment. The comprehensive strength of the manufacturer directly determines the equipment adaptability, operation stability and post-service guarantee. The core dimensions of the selection are classified as follows:

    • Industry special project experience: give priority to verifying similar landing cases of suppliers in carbon products, anode processing and chemical high-risk explosion-proof scenarios, focus on benchmarking project experience under the same working conditions and equipment specifications, abandon manufacturers with only general crane installation experience, and ensure that manufacturers are familiar with special working conditions and operation pain points of carbon block production.
    • Non-standard customization adaptability: there are different requirements for carbon block size, marshalling quantity, yard layout and explosion-proof zoning conditions on site, and standard models cannot be fully adapted.The supplier is required to have exclusive customization capability, which can optimize fixture structure, equipment parameters, explosion-proof configuration and control system according to actual working conditions on site, and meet the personalized production requirements of the plant.
    • Localization after-sales maintenance capability: equipment integration explosion-proof structure and intelligent automation system, maintenance professional requirements are extremely high.It is necessary to confirm that the supplier has a localized technical team and a rapid response mechanism, which can provide a full set of services such as on-site maintenance, fault handling, parts replacement, system commissioning, etc. to avoid long-term downtime caused by equipment failure.
    • Transparency of compliance certification: regular manufacturers shall actively and completely provide a full set of official materials such as explosion-proof certificates, safety inspection reports, equipment qualification documents, etc., eliminate problems such as lack of qualification and supplementary qualification, and ensure that equipment is put into operation in compliance with regulations and smoothly passes factory and safety supervision inspections.

    Henan mine crane as China lifting equipment leading high-tech enterprises, has a professional R & D platform and a number of patented technologies, with strong non-standard customization and complex working conditions adaptation capacity.

    The company has a complete intelligent manufacturing industry chain, leading the production and sales scale of gantry cranes in the industry, and the products are exported to many countries around the world. They are mature and suitable for high-risk and complex conditions such as carbon products, aluminum electrolysis, chemical explosion prevention, etc.

    Conclusion

    The selection of carbon block stacking crane needs to accurately match four core conditions: carbon block handling parameters, factory explosion and corrosion risk level, automation requirements and professional industry suppliers.Blind reduction and simplification of explosion-proof and anti-corrosion configuration can reduce initial investment, but it will significantly increase safety hazards and shutdown losses.

    Key parameters such as explosion-proof grade and carbon block specifications of the factory shall be specified in advance before procurement, so as to facilitate the manufacturer to provide accurate and compliant equipment solutions.When selecting partners, priority shall be given to checking similar project cases of carbon products and chemical high-risk working conditions, and professional suppliers with special customization and practical operation capability shall be accurately selected.

    Henan Mine CraneDiscuss your requirements ↗
  • How to choose a bridge double girder crane for steel plants?

    How to choose a bridge double girder crane for steel plants?

    How to choose a bridge double girder crane for steel plants?

    The operating environment in a steel plant is far harsher than that of an ordinary workshop – high temperatures, dusty conditions, mostly 24-hour continuous operation, and frequent lifting of heavy loads such as billets, coils, scrap, etc. The choice of a bridge double girder crane is crucial to the smoothness of production. Selecting the right overhead double girder crane is crucial to the smoothness of production

    Many buyers are prone to fall into a misunderstanding, think that the selection of cranes only look at the rated lifting capacity is enough. In fact, not, steel plant crane selection, the core is to match the production process, to adapt to the harsh working conditions, but also take into account the reliability and full life cycle cost, so as to really help the production.

    Next, I will combine many years of experience in steel plant crane selection, step by step to make it clear to you, how to choose the right bridge double girder crane for your factory.

    First clear crane application scenarios in the steel plant

    The operational needs of different regions vary greatly, the first application scenarios down, the selection will not be biased. The most common scenarios are mainly in these categories:

    Scrap charging and raw material field processing, which is the starting point of steel production, the need for cranes to frequently lift scrap, with the hopper to the blast furnace charging, the crane’s lifting speed and durability requirements are high, but also often need to be used with grapples.

    Billets, ingots, slabs processing, this type of load is regular shape but large weight, mostly in the rolling shop, continuous casting workshop, the crane needs to be accurately positioned to avoid collision, and sometimes use special spreader to ensure the stability of lifting.

    Steel coil handling, whether it is semi-finished or finished steel coils, need special spreader, such as C-shaped hook, not only to ensure that the coil does not slip, but also to avoid damage to the surface of the coil, mostly used in cold rolling, hot rolling workshop and finished product warehouse.

    Workshop equipment maintenance and installation, this type of operation is infrequent, but the load is uncertain, sometimes need to lift heavy equipment parts, the flexibility and versatility of the crane requires a high degree of flexibility and versatility, generally with a common hook can be.

    Finished product warehouse loading and unloading, mainly responsible for the finished steel coils, steel plates, etc. lifting to the transport vehicle, need to take into account the efficiency and accuracy, to avoid damage to the finished product, often with a special spreader and remote control operation.

    There are also steel-related areas (such as steel ladle lifting), this type of scene is a high-risk operation, the requirements of the crane is much higher than the ordinary workshop, need to be designed in accordance with the special standards of metallurgical cranes, additional safety protection measures.

    Why do we need to clarify the application scenarios first?

    Differences in working conditions in different application areas directly determine the core requirements of the crane, which may affect the use of a little worse. For example, high-temperature areas and ordinary workshops, the heat resistance requirements for cranes are completely different.

    Temperature, near the steel package, hot rolling workshop temperature is very high, there will be radiant heat, crane cables, motors, brakes need special heat-resistant design, otherwise it is easy to age and damage; and raw materials field, finished goods warehouse temperature is relatively mild, conventional configuration can be.

    Speed and positioning accuracy, billet, steel coil transfer needs accurate positioning, speed can not be too fast, but also has a smooth acceleration and deceleration function; and scrap steel charging is more important to the lifting and running speed, improve operational efficiency.

    The choice of spreader is also directly related to the application scenario, the grab is suitable for scrap, C-hook is suitable for steel coils, billet needs to use the lifting tongs or lifting beams, choose the right spreader in order to ensure the safety and efficiency of the operation.

    Here is a special reminder: steel ladle and other molten metal lifting crane, does not belong to the conventional bridge double girder crane, must comply with the special standards of metallurgical cranes, but also equipped with redundant braking, emergency descent and other additional safety devices, can not be replaced by ordinary workshop cranes.

    Before selecting the type, first collect the site and process data

    Many purchasers only give a rated lifting capacity and span when selecting a model, which can easily lead to the crane does not meet the actual use of demand, and even rework and return.

    Load Characteristics: Define what to lift and how much to lift

    First of all, to determine the rated load and maximum load, here is an easy to ignore the point: the rated lifting capacity of the crane, need to include the weight of the spreader.

    Also pay attention to the size and centre of gravity of the load, such as the inner diameter, outer diameter, width of the steel coil, the length of the steel billet and the cross-section size, which will affect the choice of spreader and the positioning accuracy of the crane.

    In addition, whether hot or ambient material is being lifted makes a big difference.

    The lifting method is also very critical, whether it is a single point lifting or with special lifting tools (such as C-hooks, lifting tongs, electromagnetic suction cups, grabs, lifting beams), different lifting methods, the crane lifting mechanism, wire rope configuration have different requirements.

    Work cycle and mode of operation

    Most of the iron and steel mills are multi-shift continuous production, the crane’s operating intensity is very high, which requires a clear understanding of its work cycle parameters, to avoid the selection of ‘underestimation’ of the intensity of the operation, resulting in early wear and tear of the crane.

    For example, how many shifts per day, how long each shift runs, how many times per hour, these data directly determine the crane’s work level (-duty class). The more frequent the operation and the higher the load, the higher the duty class needs to be.

    Also pay attention to the intensity of the peak production period, such as the peak of steelmaking, the crane may need to run continuously at full load, this time if the crane’s working level is not enough, it is easy to motor overheating, brake wear and tear too fast and other problems, which will lead to downtime.

    Factory environment: the test of cranes in harsh environments

    The environment of the steel plant has a great impact on the durability of the crane, especially the three factors of high temperature, dust and corrosiveness, which must be focused on.

    High-temperature environment is mainly concentrated in the hot rolling shop, steel ladle lifting area, in addition to ambient temperature is high, there is also radiant heat, the need to equip the crane’s motor, brake, electrical control cabinets with heat dissipation devices, cables should be selected to resist high temperature models, and, if necessary, to be added to the heat shield.

    Dust and oxidised skin are common problems in steel mills. Dust can get into the bearings, gears and electrical parts of cranes, leading to wear and tear and failure.

    Corrosive environments are mainly found in pickling lines, chemical treatment areas, and steel mills in coastal areas, where corrosive gases or seawater can corrode the metal structure and electrical components of cranes.

    It is also important to clarify whether the crane is installed indoors, semi-outdoors or outdoors. Outdoor installation requires consideration of rain and wind protection measures to avoid bad weather affecting crane operation.

    Installation constraints: plant conditions determine the size limit of the crane

    Many steel mills are retrofit projects, the original plant structure of the limitations, will directly affect the selection of the crane, confirm these parameters in advance, to avoid the crane transported to the site can not be installed.

    Firstly, the plant span and track length, the crane span must match the plant span, the track length should be determined according to the scope of the operation area, but also reserve a certain safety margin.

    Clearance height is another key parameter, the height of the beam bottom of the plant, pipelines, platforms, lighting equipment, etc., will affect the lifting height of the crane and the range of hook activity, you need to measure the exact clearance height to avoid the crane installation can not reach the required lifting height.

    If it is a retrofit project, it is also necessary to check the condition of the original track beams, such as the carrying capacity of the track beams, alignment, if the track beams are not sufficiently load-bearing, they may need to be reinforced, otherwise there will be potential safety hazards

    In addition, it is also necessary to confirm the power supply capacity and stability of the plant, the crane’s motor and control system need stable power supply, voltage fluctuation is too big to affect the normal operation of the crane, or even damage the electrical components.

    Why steel mills prefer overhead double girder cranes

    In the heavy-duty operation of steel mills, the usage rate of overhead double girder cranes is much higher than that of single girder cranes, not because it is more ‘advanced’, but because it is better suited to the harsh working conditions of steel mills.

    Structural and operational advantages

    Firstly, the double girder structure has a stronger load carrying capacity, which is more suitable for the high load and large span requirements of steel mills. For example, when lifting heavy billets and coils, or large tonnage scrap grabs, double girder cranes have a stronger metal structure with better rigidity, which can withstand greater impacts and be more stable during operation.

    Secondly, double girder cranes are easier to integrate maintenance platforms and walkways. Cranes in steel mills require regular maintenance, and maintenance platforms allow staff to more safely and conveniently inspect and repair the crane’s hoisting mechanism and electrical components, reducing maintenance difficulties and safety risks.

    Double girder cranes also have advantages in terms of hook travel and space utilisation. Many double girder cranes have hooks that can be closer to plant columns and higher lifting heights, making full use of plant space, especially suitable for retrofit of old plants with limited space.

    In addition, double girder cranes have better operational stability and can reduce shaking, position accurately and avoid load collision during continuous high load operation, which is crucial for precision operations in steel plants.

    When is a single girder crane not enough

    Although single girder cranes are cheaper and simpler to install, there are many scenarios in steel mills where the performance of single girder cranes cannot meet the demand.

    If the intensity of the operation is high and multiple shifts are run continuously every day, the structure and mechanism of the single girder crane are prone to early wear and tear and failure; if the load to be lifted is heavy or needs to be paired with a large lifting device (such as a large tonnage grab or electromagnetic suction cup), the load carrying capacity and stability of the single girder crane will be insufficient.

    There are also some scenarios that require precise positioning, such as the stacking of steel coils, billet rolling assistance, single girder cranes do not have enough operational precision and stability, which can easily lead to load offset, collision, affecting production efficiency and product quality.

    Simply put, in steel mills, as long as it involves high loads, high operating intensity and precise positioning scenes, double girder cranes are preferred in order to ensure long-term stable operation.

    Core technical parameters must be correctly defined

    Technical parameters are the core of crane selection, each parameter directly affects the performance of the crane and the use of the effect, can not be estimated empirically, must be combined with the actual needs of the site to determine.

    Lifting capacity (SWL)

    Lifting capacity is the most basic parameter, but can not only look at the rated load, but also consider the actual operation of various situations. For example, in addition to the weight of the material to be lifted, the weight of the spreader must also be added, which is easily ignored.

    The load situation of different processes is also different, such as lifting steel coils and lifting steel billets, the load is stressed in different ways; lifting bundles of steel billets and single billets, the weight distribution is also different, you need to determine the rated lifting capacity of the crane according to the actual load situation.

    Also consider the dynamic load, crane lifting, running, braking, the load will produce inertia force, resulting in the actual force is greater than the static load, the selection needs to be reserved for a certain margin of safety.

    Span

    The span of the crane, that is, the distance between the two rails, must be matched with the span of the plant, can not be arbitrarily determined. Firstly, the actual span size of the plant should be checked, and then the span of the crane should be determined according to the scope of the operation area.

    Attention should also be paid to the safety gap when the crane is in operation, for example, between the end beams of the crane and the columns of the plant, and between the crane and other equipment, it is necessary to reserve a certain gap to avoid collision during operation.

    If it is a retrofit project, the span of the original track must be checked to ensure that the span of the crane is the same as the span of the track, otherwise it cannot be installed and used. The best way is to provide the actual drawing of the plant and let the supplier help to confirm.

    Lifting height/hook travel

    Lifting height refers to the distance from the lowest position to the highest position of the hook, which needs to be determined according to the operational requirements, such as the stacking height of the materials and the installation height of the equipment, all need to be taken into account.

    Also pay attention to the headroom of the plant, the highest position of the hook should not exceed the bottom of the beam of the plant, and at the same time, a certain safety distance should be reserved to avoid the hook colliding with the structure of the plant or other equipment.

    In addition, it is also necessary to consider the future process changes or equipment replacement needs, if the future may need to lift a higher load, the selection can be appropriate to increase the lifting height, to avoid the later transformation.

    Lifting, traversing and longitudinal speed

    Many buyers will blindly pursue the ‘high speed’, think the faster the efficiency is higher, but in fact, the speed of the crane needs to match the rhythm of the production process, not the faster the better.

    For example, in the scrap charging scene, the lifting and longitudinal speed can be faster, to improve operational efficiency; but in the steel coil stacking, billet positioning scene, the speed can not be too fast, otherwise it will lead to load shaking, affecting the positioning accuracy, there may also be safety hazards.

    In addition to the maximum speed, but also pay attention to acceleration and deceleration performance, smooth acceleration and deceleration can reduce mechanical impact, extend the service life of the crane, but also to avoid load collision. For scenes that require precise positioning, there should also be fine-tuning (inching) function, which is convenient for operators to control accurately.

    Work Class (Duty Class)

    Duty class is a key parameter in the selection of cranes for steel mills, which directly determines the service life and reliability of cranes and should never be underestimated.

    Duty class is determined according to the crane’s operating frequency, load status, operating time and other factors, the higher the level, the stronger the crane’s structure and mechanism, the greater the intensity of the work it can withstand.

    Cranes in steel mills, most of which require continuous high-load operation, the working level is generally not less than A6, some high-intensity operating scenarios (such as steel ladle lifting, continuous charging of scrap), you need to choose A7, A8 level, otherwise it will lead to early wear and tear of the crane, overheating of the motor, brake failure, and frequent shutdowns and failures.

    Here is a reminder: do not choose a working level lower than the actual demand in order to save costs, the later maintenance costs and downtime losses, will be much higher than the initial savings in procurement costs.

    Crane track and wheel load

    Wheel load refers to the pressure of the wheels on the track and track beam when the crane is running, this parameter is easily ignored, but it directly affects the structural safety of the plant.

    When selecting the model, the wheel load of the crane must be calculated and then checked with the bearing capacity of the track beam of the plant to ensure that the wheel load does not exceed the bearing limit of the track beam. If it is a retrofit project, the original track beam’s bearing capacity is insufficient, it is necessary to reinforce it in advance, otherwise there will be serious safety hazards.

    Wheel load also affects the wear and tear of wheels and rails. Excessive or uneven distribution of load will lead to rapid wear and tear of wheels and rails, increasing maintenance costs and even affecting the operational stability of the crane.

    Select the right hoisting mechanism and spreader

    Crane lifting mechanism and spreader, directly determines the safety and efficiency of lifting, different types of materials, need to match different lifting mechanism and spreader, can not be generalised. Many purchasers only focus on the crane itself, ignoring the choice of spreader, resulting in the later can not work properly.

    Hook: suitable for general maintenance and equipment lifting

    Hook is the most versatile spreader, suitable for workshop maintenance, equipment installation, general cargo lifting and other scenarios, such as lifting crane parts, small equipment, scattered materials.

    The advantage of this kind of spreader is flexible, can adapt to a variety of loads, but for the repetitive material lifting in steel mills (such as steel coils, billets), the efficiency is not high, and is not safe enough, it is not recommended as the main spreader.

    C-hook: the first choice for steel coil lifting

    C-hooks are the most commonly used and practical spreader for lifting steel coils, both cold rolled and hot rolled coils. It can directly hook the inner diameter of the steel coil, stable during the lifting process, not easy to slip, but also to avoid damage to the surface of the steel coil.

    When choosing C-hooks, you need to determine the size and load capacity of C-hooks according to the inner diameter, outer diameter, width and weight of the steel coils to ensure that it matches the steel coils. For example, different sizes of steel coils with different inner diameters require different types of C-hooks, which cannot be used universally.

    Clamps, clamps, lifting beams: special lifting tools for billets and slabs

    When lifting billets, ingots, slabs and other long, lumpy materials, it is suitable to use lifting tongs, jigs or beams. This kind of spreader can firmly clamp or hold the material to avoid the material slipping off during the lifting process, and at the same time, it can ensure the uniform force of the material and reduce the damage.

    For example, a single billet can be lifted with a lifting tongs, lifting a number of billets or slabs, you can use a lifting beam with a number of lifting tongs, to improve operational efficiency. When choosing this kind of spreader, according to the size, weight and shape of the material, determine the type and quantity of spreader to ensure the safety of lifting.

    Electromagnetic suction cups: suitable for lifting scrap steel and steel plates

    Electromagnetic suction cup is suitable for lifting scrap steel, steel plate, small billet and other materials, the advantage of high efficiency, can quickly adsorb and release the material, do not need artificial hook.

    But the use of electromagnetic suction cups have a few precautions: firstly, need a stable power supply, once the power failure, the material will fall, there is a safety hazard, so must be equipped with a backup power supply or emergency device; Secondly, the electromagnetic suction cup adsorption force and the weight of the material to match, to avoid adsorption of the material is not firmly caused by the material slipping; Finally, the high temperature of the material will affect the adsorption performance of electromagnetic suction cups, is not suitable for lifting the hot material.

    Grab: special spreader for scrap charging

    In the scrap yard and blast furnace charging area, grab is an essential spreader, which can quickly grab the scrap and improve the charging efficiency. There are many types of grabs, such as single-rope grabs and double-rope grabs, which need to be selected according to the type of scrap and operational requirements.

    The work intensity of the grab is very high, need to match the high strength lifting mechanism, at the same time, we should do a good job of maintenance of the grab, regularly check the wear and tear of the grab, to avoid damage to the grab resulting in the scattering of scrap steel.

    Here to give you a practical advice: crane and spreader selection should be synchronised, do not buy a crane first, and then select a separate spreader. The weight of the spreader, the installation method, will affect the crane lifting mechanism and carrying capacity, synchronised selection can avoid mismatch problems later.

    Steel plant environment on the special requirements of the crane

    The harsh environment of steel mills is one of the main causes of crane failure. Many cranes can run stably for many years in ordinary workshops, but frequent failures in steel mills, just because they do not consider the impact of the environment and do not do a good job of targeted protection.

    High temperature and radiant heat

    Cranes in high-temperature areas should first do a good job of heat-resistant protection of electrical components. Motors, brakes, electrical control cabinets and other components, to choose high-temperature resistant models, while equipped with heat dissipation devices, such as forced ventilation fans, cooling water pipes, to avoid parts due to high-temperature aging, damage.

    Cables should also use high-temperature resistant cables, and should be well protected to avoid being scalded by high-temperature oxidised skin or accelerated aging by high-temperature environment. In the area near the steel package and other strong radiant heat, but also to the crane’s metal structure and electrical components to add a heat shield to reduce the impact of radiant heat.

    In addition, high temperature environment, the viscosity of the lubricant will be reduced, the lubrication effect will be reduced, the need to use high temperature resistant lubricants, and shorten the lubrication cycle, to ensure that the moving parts of the crane is well lubricated.

    Dust, oxide skin and pollution

    Dust and oxidised skin from the steel mill will enter the bearings, gears, wire ropes and electrical parts of the crane, leading to wear and tear of the parts, jamming and short-circuiting and affecting the normal operation of the crane.

    Therefore, the key components of the crane need to be well sealed and protected, such as the electrical control cabinet to choose IP54 and above grade sealing, to avoid dust entry; bearings, gears and other moving parts, to be installed with a sealing cover, to prevent dust and oxidised skin from entering; wire ropes should be cleaned and lubricated on a regular basis, to avoid dust abrasion of the wire ropes.

    Cranes should also be cleaned regularly to remove dust and oxidised skin on the surface, especially electrical parts and moving parts, to avoid excessive accumulation of dust leading to failure.

    Corrosion protection

    First of all, the metal structure should be anti-corrosion treatment, such as sandblasting rust removal, painting corrosion-resistant coatings, paint layers and thickness should be determined according to the degree of corrosion and sealing to prevent corrosive gases from entering.

    Power supply quality and electrical stability

    The normal operation of the crane requires a stable power supply, more production equipment in steel mills, prone to voltage fluctuations, which will affect the electrical system of the crane, resulting in motor burnout, control system failure.

    When selecting the type, we should consider the impact of voltage fluctuations, choose motors and control systems that can adapt to a certain voltage fluctuations, and at the same time, equipped with voltage protection devices, such as voltage regulators, over-voltage protectors, to avoid voltage fluctuations on the crane damage.

    Drive and control system

    Drive and control system, determines the crane’s operating performance and ease of operation, selection should not only consider the process requirements, but also combined with the factory’s maintenance capabilities, to avoid choosing too complex, difficult to maintain the system.

    Variable frequency (VFD) control vs conventional control

    At present, most of the cranes in steel mills use variable frequency control (VFD), which has obvious advantages over conventional control.

    Secondly, VFD control can achieve stepless speed regulation, adjusting the speed according to the operational requirements, which not only improves the efficiency, but also ensures accurate positioning.

    In addition, frequency control saves energy, especially in the crane frequent start and stop, load changes in the scene, energy saving effect is more obvious.

    Conventional control is low-cost and simple to maintain, suitable for low intensity operations, low requirements for speed and positioning accuracy of the scene, such as small maintenance cranes.

    Selection of speed control strategy according to application scenarios

    Different application scenarios require different speed control strategies and cannot be generalised. For example, scrap charging, finished product loading and unloading and other scenes, the need for rapid transit, lifting and running speed can be faster; while billet positioning, equipment installation and other scenes, the need for precise control, the speed should be slower, but also fine-tuning function.

    For scenes that require frequent starting and stopping, choose a control system with good acceleration and deceleration performance to reduce mechanical impact; for scenes of continuous operation, ensure the stability of the control system to avoid failure.

    Operation mode

    There are three main crane operation modes: pendant control (handle control), radio remote control, and cab operation, which need to be selected according to the operational scenarios.

    Handle control is simple, low-cost, suitable for small cranes or close-range operations, such as workshop maintenance cranes, but the operation is less flexible, the operator needs to follow the crane to move, and safety is not high.

    Radio remote control is the most commonly used mode of operation in steel mills, the operator can control the crane remotely in a safe area, with a wide field of vision and flexible operation, which can effectively avoid operational risks, especially suitable for scrap charging, steel coil lifting and transporting and other scenarios.

    The cab operation is suitable for complex, high-risk, large tonnage operation scenarios, such as steel ladle lifting, heavy equipment installation, the operator in the cab, a good field of vision, can accurately control the crane, and at the same time, higher safety.

    Many steel mills will choose multiple operation modes, such as remote control + cab operation, to ensure operational flexibility and to cope with complex scenarios, but also as a back-up to avoid downtime due to failure of one operation mode.

    Monitoring and Diagnostics: Easy Maintenance and Troubleshooting

    Once a crane in a steel plant breaks down, it will affect production. Therefore, the monitoring and diagnostic functions of the control system are important to help the staff find faults and troubleshooting in time to reduce downtime.

    For example, the fault alarm and history log function can record the fault information of the crane, which is convenient for the staff to trace the cause of the fault; the motor temperature and brake wear monitoring function can provide early warning of component wear and tear and preventive maintenance; the remote diagnostic function (if any) allows the supplier to remotely assist in troubleshooting to improve the maintenance efficiency.

    When selecting a system, you can choose a control system with appropriate monitoring and diagnostic functions according to the plant’s maintenance needs, and avoid choosing a system that is too simple and has no monitoring functions, otherwise troubleshooting will be very difficult in the later stages.

     Compliance and Redundancy

    Crane operations in steel mills are high-risk, and safety is the top priority. When selecting a crane, you should not only consider the performance of the crane, but also ensure that the crane complies with safety standards and has sufficient safety protection measures to avoid safety accidents.

    Necessary safety devices

    Regardless of the scenario of the crane, the following safety devices are necessary and indispensable:

    Overload protection device, which can prevent the crane from overload operation, avoiding structural damage and safety accidents

    Upper and lower limit switches to limit the lifting and lowering range of the hook, preventing the hook from colliding with the crane structure or the ground.

    Emergency stop system, which can quickly stop the crane operation in case of emergency to avoid the accident from expanding.

    Running limit switches and buffers, which can limit the running range of the crane and prevent the crane from colliding with the ends of the track or other equipment

    Anti-collision protection device, if there are more than one crane on the same track, must be equipped with anti-collision device to prevent collision between cranes.

    Load display and warning system, which can display the weight of the lifting load in real time, and issue an early warning when the load is close to the rated value to remind the operator to pay attention

    Brake monitoring device, which is recommended for high work intensity scenarios, can monitor brake wear and warn of failures in advance.

    Additional safety requirements for high-risk, high-temperature areas

    For high-risk scenarios such as ladle lifting and high-temperature areas, in addition to the necessary safety devices, additional safety measures need to be added to improve safety.

    For example, equip redundant brakes or safety brakes, so that even if the main brake fails, the back-up brake can act as a brake to prevent the load from falling down

    Adding thermal protection to electrical components to prevent damage from high temperatures, and equipping emergency lowering devices that can manually lower the load safely in the event of a power failure or malfunction to avoid accidents.

    Also set up interlocking devices with plant equipment and area entrances, such as steel ladle lifting area, the crane can only operate when no one is in the area and the equipment is in a safe condition, to avoid personnel accidentally entering the dangerous area.

    Standards and Compliance

    The selection and installation of cranes must comply with local regulations and standards, and also meet the internal technical standards of the plant to avoid non-compliance.

    Metallurgical cranes, for example, must comply with special standards for metallurgical cranes and cannot be replaced by ordinary cranes;

    The manufacture, installation and commissioning of cranes must be completed by enterprises with appropriate qualifications to ensure quality and safety.

    Also pay attention to the inspection, commissioning and documentation requirements, the crane installation is completed, you need to pass the inspection by a professional organisation before it can be put into use

    Suppliers need to provide complete technical documentation, inspection reports, operating manuals, etc., to facilitate late maintenance and inspection.

    Track, structure and installation

    Many purchasers in the selection, only focus on the purchase price of the crane, ignoring the track, structure and installation links, resulting in hidden costs in the later stage, such as track reinforcement, installation stoppages, rework, etc., but increased the total expenditure.

    Carrying capacity and alignment of track beams

    The track beam is the foundation of the crane, and its carrying capacity and alignment directly affect the operational safety and service life of the crane. If it is a retrofit project, the condition of the original track beam must be checked in advance, such as whether the load carrying capacity meets the wheel load of the crane and whether the track alignment meets the requirements.

    If the track beam has insufficient bearing capacity, reinforcement is required, and the reinforcement cost is often not low; if the track alignment is insufficient, it will lead to deflection when the crane is running, and the wheels will wear out too fast, which will increase the maintenance cost and even affect the normal operation of the crane.

    It is recommended that at the early stage of selection, structural engineers should be asked to account for the track beams to determine whether reinforcement or adjustment is required, to avoid reworking when problems are found at a later stage.

    Headroom height and plant interference

    The headroom height of the plant, pipelines, platforms, lighting equipment, etc., will affect the installation and use of the crane, verify these parameters in advance, can avoid the crane can not be installed after delivery to the site.

    Also consider the maintenance space of the crane, such as the top and side of the crane, you need to reserve enough space to facilitate the staff to carry out maintenance and overhaul, otherwise the maintenance will be very difficult later.

    Installation and shutdown planning

    The production continuity of the steel plant is very strong, the installation and commissioning of the crane, it is easy to affect the production, therefore, it is necessary to do a good job in advance of the installation and shutdown planning to reduce the production interruption time.

    If it is a new plant, crane installation can be synchronised with the construction of the plant to avoid later installation affecting production;

    If it is a retrofit project, it is necessary to choose a suitable downtime window, such as the production off-season, maintenance period, to minimise the installation and commissioning time.

    Detailed installation and lifting programmes also need to be developed to ensure that the installation process is safe and efficient, and to avoid accidents during installation, which can further extend downtime.

    Total Life Cycle Cost (TCO)

    Many purchasers only compare the purchase price of cranes when selecting a model, thinking that the lower the price, the more cost-effective. However, in steel mills, cranes have a long service life, and later maintenance costs, energy consumption, downtime losses, etc., are much higher than the purchase price of the first stage, so the total life cycle cost (TCO) is a more important selection index.

    Capital expenditure (CAPEX)

    CAPEX includes not only the price of the crane itself, but also the following aspects, the selection needs to be a comprehensive comparison, not just a single crane price:

    The price of the crane body and lifting, trolley system; the price of the spreader (e.g., C-hooks, grabs, electromagnetic suction cups, etc.);

    The price of the electrical and control system, such as frequency control is more expensive than conventional control, but it can save energy consumption in the later stage; the installation and commissioning costs, including the cost of crane installation, track reinforcement, commissioning and so on.

    There are also track modification, structural reinforcement costs (retrofit project); operators and maintenance personnel training costs; technical documentation, inspection reports and other costs. These costs add up to the total capital expenditure of the crane.

    Operating Expenditure (OPEX)

    Operating expenditure refers to the annual costs incurred after the crane is put into use, this part of the cost will be accompanied by the entire service life of the crane, need to focus on:

    Energy consumption costs, the crane’s motor power, running time, control mode, will affect the energy consumption, frequency control of the crane, energy consumption is lower than the conventional control of 10-30%, the long-term can save a lot of money; wear parts replacement costs, such as wire rope, wheels, brakes, contactors, etc., these parts need to be replaced regularly, the better the quality of the parts, the longer the replacement cycle, the lower the expenditure in the later stage.

    Preventive maintenance costs, including lubricants, maintenance labour and other costs, regular maintenance can extend the service life of the crane and reduce the breakdown downtime; spare parts consumption and procurement cycle, the longer the procurement cycle of spare parts, the more likely to lead to prolongation of downtime, therefore, you need to choose the supplier with sufficient supply of spare parts and short procurement cycle.

    Downtime loss, this is the most easily ignored cost, once the crane fails, it will lead to the interruption of the production line, the downtime loss per hour may be up to tens of thousands of yuan, therefore, the higher the reliability of the crane, the less downtime loss.

    Life cycle reliability

    Crane reliability, directly affecting the full life cycle costs, the higher the reliability, the later the maintenance costs and downtime losses the less.

    For example: two cranes, A crane procurement price is low, but the work level is not enough, the quality of the core components is average, frequent failures in the late stage, the annual maintenance costs and downtime losses are very high; B crane procurement price is slightly higher, but the work level matches, the quality of the core components is good, few failures, maintenance costs and downtime losses are low, in the long run, the full life cycle cost of the B crane instead of lower.

    Supplier Evaluation

    Cranes in steel mills not only require reliable quality, but also need perfect after-sales service, therefore, when selecting the type, you can not only look at the supplier’s offer, but also a comprehensive assessment of the supplier’s strength, to avoid choosing a supplier with insufficient strength, and later problems can not be solved.

    Iron and steel industry project experience

    Iron and steel mills have special working conditions, the design and manufacture of cranes need to be combined with the characteristics of iron and steel production, so it is crucial for the supplier to have project experience in the iron and steel industry.

    You can ask the supplier to provide relevant cases, such as projects with other steel mills, especially those with similar processes to your own plant, such as the same cold rolling plant, billet handling, scrap charging and other scenarios.

    Suppliers with experience in the steel industry have a better understanding of the harsh environment and operational needs of steel mills, and can design more suitable cranes, and at the same time, are more experienced in installation, commissioning, maintenance, etc., and can better solve the problems that arise later.

    Engineering Design Capability: Ensure Cranes are Adapted to Site Requirements

    Many cranes in steel mills need to be customised according to on-site working conditions, so the engineering design capability of the supplier is very important. The supplier needs to be able to design a crane that meets the needs based on the factory drawings and site data, including structural design, spreader matching, control system selection, etc. The supplier can be asked to provide a detailed design plan.

    Suppliers can be asked to provide detailed design plans, assembly drawings, load tables and other technical documents to assess the supplier’s design capabilities

    At the same time, the supplier needs to be able to assist in checking the load capacity of the track beam, headroom height, etc., and give reasonable suggestions to avoid selection errors.

    If the crane needs to be integrated with the factory’s control system, the supplier also needs to have the appropriate integration capabilities to ensure that the crane can be linked with the factory’s production system to improve operational efficiency.

    Manufacturing and quality assurance

    The quality of the crane directly affects its reliability and service life, so it is necessary to assess the supplier’s manufacturing capacity and quality assurance system.

    You can learn about the supplier’s production scale, production equipment, welding process, etc. Welding quality is the key to the safety of the crane structure, which requires the supplier to have a perfect welding quality control system and provide welding quality records.

    Factory acceptance test (FAT) is also very important, before the crane leaves the factory, it is necessary to carry out factory acceptance test, check the performance of the crane, safety devices, control systems, etc., to ensure that the crane meets the design requirements, the supplier needs to co-operate with the completion of the FAT test, and to provide test reports.

    In addition, suppliers need to provide traceability records of key components and materials to ensure the quality of components and materials and avoid using inferior components.

    Installation and after-sales service

    Installation and after-sales service is the guarantee of later use, the supplier needs to have a professional installation team, can complete the installation and commissioning of the crane according to the plan, to ensure that the crane is normally put into use.

    After-sales service, the supplier needs to provide operators and maintenance personnel training to ensure that the staff can operate and maintain the crane correctly.

    Need to provide sufficient spare parts to ensure that spare parts can be supplied in a timely manner; need to have a perfect service response mechanism, commitment to respond to faults within the specified time, send technicians to solve the problem on-site.

    If the supplier can provide remote diagnostic services, it is even more advantageous to remotely assist in troubleshooting and reduce downtime.

    A few questions you must ask the supplier before purchasing

    1. what is the working level of the crane you choose for us?

    2. Do you include the weight of the spreader when calculating the lifting capacity of the crane?

    3. what is the wheel load of the crane?

    4. what is included in the quotation?

    5. what is the lead time for delivery?

    6. what is the lead time and price for spare parts?

    7. how long does it take to install and commission the crane?

    8. how long is the response time for after-sales service?

    10 common misunderstandings in the procurement of double girder cranes for steel mills

    1. Only look at the procurement price, ignoring the full life cycle cost. Many purchasers choose low-priced, poor-quality cranes in order to save up-front costs, and the later maintenance costs and downtime losses are much higher than the up-front savings.

    2. Use the specifications of ordinary workshop cranes for high load operations in steel mills. Ordinary workshop cranes, working level, heat resistance, protection level do not meet the needs of steel mills, and are prone to failure.

    3. ignoring the weight of the spreader when calculating the lifting capacity. The actual lifting capacity is not enough to lift the material properly, and even there is a potential safety hazard.

    4. Underestimate the impact of high temperature and dust on crane components, without proper targeted protection. Resulting in rapid aging, damage to crane components, frequent failures.

    5. do not check the bearing capacity and alignment of the track beam at the early stage of selection, and later found that the track beam can not withstand the load of the crane, need to be reinforced, increasing the hidden costs.

    6. Excessive attention to the maximum speed of the crane, ignoring the actual process rhythm and positioning accuracy. Resulting in unstable crane operation, load collision, affecting productivity and product quality.

    7. According to the ‘normal’ intensity of work to choose the level of work, ignoring the peak production period of the intensity of work. Lead to the crane in the peak period of full-load operation, early wear and tear, failure. 8.

    8. Choose too complex control system, beyond the factory’s maintenance capacity. In case of failure at a later stage, it is impossible to troubleshoot and repair in time, prolonging the downtime.

    9. There is no clear requirement for spare parts supply and after-sales service. When the crane breaks down at a later stage, the spare parts cannot be supplied in time, and the supplier does not respond in time, resulting in prolonged downtime.

    10. Cranes and spreaders are purchased separately without synchronised selection.

    As a result, the spreader is not matched with the crane and cannot operate normally, and even need to re-procure the spreader.

    Simple and practical selection process

    First determine in which area the crane is to be installed and what materials are to be lifted.

    Collect process, load and environmental data

    Collect detailed site data, including the weight, size and centre of gravity of the load, the number of operating shifts, the lifting frequency, the temperature, dust and corrosion of the plant, the carrying capacity of the track beams, the headroom height, etc., to ensure that the data is accurate.

    Determine the lifting method and spreader type

    According to the type of material to be lifted, determine the type of spreader, and at the same time determine the lifting method, and simultaneously consider the weight of the spreader.

    Determine core technical parameters

    According to the collected data and lifting requirements, determine the core parameters of the crane such as rated lifting capacity, span, lifting height, operating speed, working level, etc., to ensure that the parameters match the actual requirements.

    Check the track and plant constraints

    Check the carrying capacity and alignment of the track beams, the headroom height of the plant, and the layout of the equipment, etc., to ensure that the crane can be properly installed and operated, and carry out track reinforcement or adjustment if necessary.

    Compare controls, safety options and total life cycle costs

    According to the process requirements, select the appropriate control system (variable frequency or conventional) and operation mode, and determine the configuration of the safety devices; compare the whole life cycle costs of different options and select the most cost-effective option, do not just look at the purchase price.

    Evaluate the strength of suppliers

    Screen suppliers with experience in the steel industry, strong engineering design capability, guaranteed quality and perfect after-sales service; compare suppliers’ offers and solutions, and conduct on-site inspections.

    Clarify the technical scope and implementation plan

    And the supplier to clarify the technical specifications of the crane, implementation details and service commitments, Henan Mine Crane manufactured many years of deep ploughing into the steel industry crane R & D, with excellent quality, customised solutions and perfect after-sales service, to match the iron and steel plant high temperature, high load demanding conditions, we invite you to join hands with Henan Mine Crane, choose the right double girder crane, build the foundation of the production, and jointly promote the high-quality development of the iron and steel industry!

    Henan Mine CraneDiscuss your requirements ↗
  • How to choose a bridge double girder crane for chemical plants?

    How to choose a bridge double girder crane for chemical plants?

    How to choose a bridge double girder crane for chemical plants?

    The production environment of chemical plants is fundamentally different from that of ordinary industrial scenes, with all kinds of flammable and explosive gases and vapours, as well as highly corrosive acids, alkalis and solvents, spreading over all aspects of production and maintenance.
    As the core equipment for equipment lifting and maintenance in the plant, the bridge crane must not be used in ordinary industrial models, and the special double girder overhead travelling crane suitable for chemical industry conditions is the inevitable choice.

    bridge double girder crane for chemical plants(

    bridge double girder crane for chemical plants

    If you use standard industrial cranes in chemical plants, not only due to the lack of explosion-proof, corrosion-resistant design, very easy to cause spark explosions, rapid corrosion failure of equipment and other safety incidents, but also due to non-compliance with industry safety standards to face regulatory penalties.
    In the selection of cranes for chemical plants, compliance, anti-corrosion capacity and operational safety, is the core principle throughout, and the design characteristics of the double girder structure is just right to match the chemical plant’s heavy lifting, complex working conditions of the multiple needs.

    In this field, Henan Mine Crane has a wealth of practical experience, as a deep ploughing lifting machinery field for many years the strength of the enterprise, the production of chemical double girder overhead travelling crane, fit all kinds of chemical conditions of customised needs, has for a number of petrochemical, organic chemical enterprises to provide suitable equipment solutions, has accumulated a large number of mature cases, it is worthwhile to refer to.

    Why chemical plants give priority to double girder overhead travelling crane?

    In the chemical industry, double girder overhead travelling crane is always the mainstream choice for equipment lifting and production support operations. This is not a single specification choice, but is determined by the operational needs of chemical plants and the advantages of double girder structure. Compared with single girder cranes, the double girder structure can accurately match the production and overhaul scenarios of chemical plants due to its characteristics of load bearing, height and operational durability.

    Higher lifting capacity and operational stability

    Chemical plant production is inseparable from all kinds of heavy equipment, from tens of tonnes of reactors, tanks, to large pumps, heat exchangers, the installation, relocation and overhaul of these equipment, the crane needs to have enough lifting capacity.
    The main girder of double girder overhead travelling crane adopts double track design, which has much higher loading capacity than single girder equipment of the same specification, and can easily cope with the lifting demand of heavy chemical equipment.

    At the same time, the double girder structure is more rigid, less deflection during heavy load operation, and no obvious deformation of the main girder will occur. When lifting heavy equipment, the swaying amplitude of the equipment can be effectively controlled, which not only ensures the smoothness of the lifting process, but also avoids the collision of the equipment with the pipelines and frames of the plant, which is especially important for chemical plants with dense pipelines.

    Henan Mine Crane for chemical heavy lifting needs, optimize the main beam structure of the double girder overhead travelling crane, the use of high-quality steel overall welding process, non-destructive flaw detection and strength testing, stable load carrying capacity, can adapt to 1-300 tons of load demand, the production of double girder equipment in a number of large-scale chemical projects, successfully completed the long-term lifting operation of 20-50 tons of reactors, the stability of the operation of the customer has been highly recognized. Highly recognised by customers.

    chemical plant crane

    chemical plant crane

    Larger lifting height

    The layout of chemical plants is mostly multi-storey structure, the production equipment may be distributed on different floors of the process platform, the equipment in the storage tank area and reaction area is also mostly installed in the vertical position, which has higher requirements on the lifting height of the crane’s hook. The structural design of double girder overhead travelling crane can achieve greater effective lifting height, and the operating range of the hook can cover the lifting points of multi-storey process platforms and high vertical equipment.

    Whether it is lifting heavy equipment from the ground to the second-floor process platform or overhauling and hoisting storage tanks at high altitude, the double girder overhead travelling crane’s lifting height meets the demand without the need to build additional lifting brackets, which not only improves the operational efficiency, but also reduces the safety hazards of on-site operation.

    Suitable for heavy-duty continuous operation

    The production of chemical plants is continuous, and equipment maintenance is mostly planned for short-term operations, which requires cranes to be able to respond to lifting needs at any time, and to withstand frequent start-stop operations. At the same time, part of the chemical production chain of equipment maintenance frequency is high, cranes need to participate in various types of long-term small maintenance lifting, operating load is not low.

    The overall structure and core components of the double girder overhead travelling crane are designed according to the heavy duty operation standard, which can adapt to the high frequency of lifting operations in chemical plants, whether it is the production of supporting equipment shifting, or unexpected equipment overhaul, can run stably, and provide reliable lifting support for the continuous production of the plant. Henan Mine Crane’s double girder equipment is equipped with motors and brakes in accordance with heavy-duty operation standards, which can easily cope with the needs of 24-hour continuous operation in chemical plant areas, and has outstanding batch delivery capacity, with an annual production capacity of 500-600 units of various types of overhead travelling cranes.

    double girder bridge crane

    Step 1 – Define the actual working environment of the plant

    The first step in the selection process is not to look at the equipment parameters, but to understand the operating environment of the chemical plant. The environment of chemical production varies greatly, with different workshops having different hazard levels, corrosion, temperature and humidity. Only by accurately defining the environmental characteristics can the subsequent selection of equipment be accurately adapted to avoid a ‘one size fits all’ selection error.

    Classification of hazardous areas

    One of the core risks of chemical plants is flammable and explosive, need to be based on the type of plant media, according to ATEX or local equivalent standards to complete the classification of hazardous areas, mainly divided into Zone 1 and Zone 2, the explosion-proof requirements of the two types of areas have clear differences.

    Zone 1 is the area where explosive gas environment occurs continuously or exists for a long time, such as the reaction kettle area of petrochemical plants and the periphery of oil and gas transmission pipelines; Zone 2 is the area where explosive gas environment occurs occasionally, such as the loading and unloading area of the chemical raw material warehouse. In addition to the risk of gas explosion, coal chemical industry, powder chemical industry and other workshops there is also a risk of dust explosion, this type of regional equipment selection also need to take into account the requirements of dust explosion-proof, can not only be designed according to the gas explosion-proof standards.

    Henan Mine cranes in undertaking chemical projects, will first arrange for professional and technical team to visit the survey, to assist customers to complete the classification of hazardous areas, combined with the type of media to formulate targeted explosion-proof programme, to avoid the selection deviation caused by the inability to assess the environment.

    explosion proof overhead crane for chemical plants

    Comprehensive assessment of corrosive environment

    Corrosive is another major test of the chemical environment on the crane, need to be clear in advance of the plant crane operating area in contact with the type and concentration of the media. Pickling workshop, electroplating workshop will be exposed to high concentrations of acid, alkali media, organic chemical workshop will be exposed to various types of organic solvents, and many chemical workshops will have a continuous chemical vapour, media droplet emissions, which will cause corrosion of the crane’s metal structure and electrical components.

    Different corrosive media corresponding to different protection programmes, such as strong acidic environment need to choose acid-resistant corrosion-resistant materials and coatings, organic solvent environment should consider the solvent resistance of the coating, only accurate assessment of the degree of corrosion, in order to avoid subsequent local corrosion of equipment, structural damage problems.

    Consideration of temperature and humidity conditions

    Chemical plant part of the process area there are high temperature conditions, such as ammonia, steelmaking supporting chemical workshop reaction area, the ambient temperature is much higher than the conventional industrial areas, the crane’s electrical components, lubrication system needs to adapt to the high temperature environment, to avoid aging of components, lubrication failure.

    At the same time, but also to distinguish between the crane’s operating area is indoor or outdoor, outdoor tanks, raw material loading and unloading area, will be affected by rain and snow, day and night temperature difference, humidity fluctuations, metal structure is prone to oxidation and corrosion, and indoor workshop humidity is relatively stable, but there may be a media condensation, also need to do a good job of moisture protection.

    Step 2 – Determine the explosion-proof design requirements of the equipment

    Explosion-proof is one of the core requirements of the chemical plant crane selection, especially in Zone 1, Zone 2 hazardous areas of the crane, explosion-proof design needs to cover all electrical and mechanical components, any one of the details of the negligence, may produce sparks triggered by the explosion, explosion-proof design is the core from the source to eliminate the generation and accumulation of sparks.

    The whole process of electrical explosion-proof components configuration

    The crane’s electrical system is the main source of sparks, double girder overhead travelling crane used in hazardous areas, all electrical components must be selected explosion-proof models, and explosion-proof level needs to match the regional hazard level. Explosion-proof motor is the core, and it should be of explosion-proof or safety-increasing type to avoid spark leakage when the motor is running; the control cabinet adopts explosion-proof design, and the internal wiring arrangement is standardised to prevent sparks from short-circuit of the wiring.

    Limit switches, travel switches and other electrical components that are prone to mechanical friction, you need to use spark-proof models, even lighting, junction boxes and such small parts, can not miss the explosion-proof design. The explosion-proof grade of all electrical components should be unified, and there should be no ‘high-grade parts with low-grade accessories’ to ensure the overall explosion-proof effect of the electrical system.

    Henan Mine Crane produces explosion-proof double girder overhead travelling crane, all electrical components are used in accordance with ATEX, IECEx standards of explosion-proof models, the motor adopts explosion-proof design, the control cabinet to do the full sealing of explosion-proof treatment, limit switches are used in explosion-proof models of the spark-proof, has passed the European Union CE, Russia GOST and other international certifications, as well as domestic explosion-proof certificate of conformity, to ensure that the use of the hazardous area in a compliant.

    corrosion resistant double girder crane for chemical plants

    Special design for anti-static and grounding

    Static electricity accumulation is a source of sparks easily ignored in the chemical environment, cranes in the operation process, the car body and the track, the friction between the grab and the equipment will generate static electricity, if you can’t conductive removal in time, the static electricity accumulated to a certain extent will produce static sparks, lead to gas or dust.

    Therefore, the crane needs to design a perfect anti-static grounding system, set up between the car body and the track special grounding brush, to ensure that the static electricity can be conducted in real time; cable with shielded layer of special cables, cable protection system to do a good job of sealing, to avoid cable breakage caused by the leakage of static electricity. At the same time, the metal structure of the crane to ensure electrical connectivity, to eliminate the dead space of static electricity accumulation.

    Match the relevant explosion-proof certification standards

    Crane explosion-proof design can not only stay in the structural level, but also need to obtain authoritative explosion-proof certification, which is the premise of the equipment compliance and use, but also through the subsequent plant safety acceptance of the key. The common international explosion-proof certification for ATEX and IECEx, ATEX for the EU market, IECEx for the International Electrotechnical Commission’s explosion-proof certification, a high degree of global recognition.

    In addition to international certification, it is also required to comply with local safety regulations and explosion-proof standards, such as domestic chemical companies need to obtain the explosion-proof certificate issued by the National Explosion-proof Inspection Agency. All certifications need to cover the whole equipment of the crane, rather than a single component, to ensure that the explosion-proof design of the equipment meets the standard requirements. Henan Mine Crane has successfully passed the ISO9001 quality system certification, ISO14001 environmental certification and many other qualifications, its explosion-proof crane products have a complete set of certification qualifications, can be successfully passed through the plant safety acceptance.

    Step 3 – Anti-corrosion protection and material selection

    Chemical environment corrosion will directly affect the service life of the crane and operational safety, a crane without good anti-corrosion, in the strong corrosion of the chemical workshop may be 1-2 years on the structure of the rust, component damage, and perfect anti-corrosion protection and reasonable material selection, can extend the service life of the equipment to more than 10 years. Anti-corrosion design needs to achieve ‘structural protection + material protection’ double guarantee, covering the overall structure of the crane and exposed parts.

    High-standard anti-corrosion treatment of structural surfaces

    Crane main beam, end beam, trolley frame and other metal structures, is the focus of anti-corrosion treatment, the surface treatment needs to be in accordance with the C4 or C5 anti-corrosion standards, the specific level of corrosion in accordance with the plant to determine the degree of corrosion, strong corrosive environments preferred to use the C5 level.

    The surface of the structure should be thoroughly descaled first, using sand blasting to remove rust to Sa2.5 level, to remove the surface of the oxide skin, rust and oil, to ensure that the anticorrosive paint adhesion; followed by the application of primer, paint and top coat, the primer selects epoxy zinc-rich paint, to enhance the ability of rust prevention, the top coat selects fluorocarbon paint or polyurea paint, to enhance the resistance to acid, alkali and solvents, the thickness of the painting needs to meet the standard requirements, the welded parts need to be done to avoid corrosion. Additional anticorrosive coating should be applied to the welded parts to avoid the welded gaps from becoming corrosion breakthroughs. Some of the small parts that are easy to corrode, can be hot-dip galvanised to enhance the overall anti-corrosion effect.

    Henan Mine cranes for chemical strong corrosion conditions, the use of standardized C5 anti-corrosion treatment process, the main beam by sandblasting rust to Sa2.5 level, painted zinc-rich epoxy primer + fluorocarbon topcoat, welded parts to do additional anticorrosion filler, fasteners with hot-dip galvanizing treatment, effectively slow down the corrosion of the equipment, and its anticorrosive technology has been verified in a number of strong corrosive chemical projects.

    Stainless steel or special alloy parts selection

    Crane fasteners, exposed parts, easy to wear parts, is the corrosion of the hardest-hit areas, such parts if the choice of ordinary carbon steel, very easy to rust, fracture, the need to use stainless steel or special alloy materials. Bolts, nuts, pins and other fasteners, choose 304 or 316 stainless steel, 316 stainless steel acid corrosion resistance is stronger, suitable for strong acidic environment.
    Wire ropes, hooks, pulleys and other lifting parts are made of zinc-plated or stainless steel wire ropes, and the hooks are double-protected with anticorrosive coating and stainless steel sheath.

    For strongly corrosive chemical workshops, some of the core components can be selected Hastelloy and other special alloys, although the cost of a slight increase, but can effectively avoid corrosion failure of the components, reduce the maintenance and replacement costs.
    Henan Mine cranes are strictly controlled in the selection of materials, according to the degree of corrosion of the chemical medium, the flexible use of 316 stainless steel, special alloys and other materials to ensure the corrosion resistance of components.

    chemical plant double girder crane selection

    Fully enclosed sealing design of the mechanism

    Crane running mechanism, hoisting mechanism inside the gear box, bearings, motors and other components, if the corrosive medium or water vapour, will quickly appear wear and tear, corrosion, and therefore need to adopt a fully closed mechanism design. Gear box selection of sealed type, good oil seal and dust seal, to prevent the media into the interior; electrical control cabinet using a fully sealed design, protection level of not less than IP65, the internal set of dehumidification devices, to avoid the cabinet condensation corrosion of electrical components; travelling wheels, reels and other rotating parts, the installation of protective cover, to prevent the media splash and dust accumulation.

    Henan Mine crane chemical double girder lifting equipment, are fully enclosed trolley design, gearboxes, motors and other core components sealed protection, electrical control cabinet protection level of IP65 or more, effectively blocking the intrusion of corrosive media and dust, to extend the service life of components.

    Step 4 – Approval of lifting capacity, span and structural suitability

    Crane lifting capacity, span is a basic parameter, which directly determines whether the equipment can meet the lifting requirements of the plant, while the structural suitability is related to the crane’s operational safety and the load-bearing safety of the plant, the approval of this part of the parameter needs to be combined with the plant’s equipment specifications, the layout of the plant and the building structure, and can not be based on empirical estimation alone.

    Accurately determine the actual lifting load

    When approving the lifting capacity, it is necessary to consider two types of lifting needs of chemical plants: one is the lifting of process equipment, including reaction kettles, tanks, large pumps and other fixed equipment installation and shifting, this type of load is the rated static load, and it is necessary to specify the maximum weight of the equipment; the other is the lifting load of equipment maintenance, including the dismantling of parts and components for maintenance, and the lifting of small-scale equipment, which is a small load, but with high frequency of operation, and the dynamic load of frequent starting and stopping is necessary to be considered. This type of load is small in weight, but the frequency of operation is high, and it is necessary to consider the dynamic load of frequent starting and stopping.

    The approved lifting capacity should be based on the maximum actual load, leaving a safety margin of 10-20% to avoid overloading. At the same time, the rated lifting capacity and working range of the crane should be clearly defined to ensure that the coverage and load capacity of the lifting operation are matched.

    Matching the span of the plant and load bearing requirements

    The span of the crane is determined by the column spacing of the chemical plant, and it should be approved according to the actual column spacing of the plant, and the span of the crane is generally smaller than the column spacing of the plant by 0.5-1 metre, so as to reserve a certain operating safety space and avoid collision with the columns of the plant when the crane is running.

    At the same time, the need to verify the plant’s travelling beams, cattle legs of the load-bearing capacity of the crane’s deadweight and the maximum lifting capacity of the sum, can not exceed the design load-bearing travelling beams, if the plant load-bearing is insufficient, the need to strengthen the travelling beams in advance, to avoid the later emergence of the plant structural deformation of the safety hazards. For cranes operating outdoors, it is also necessary to consider the safety distance from peripheral equipment and storage tanks to ensure that there are no obstacles in the operating range.

    Follow the industry standard of deflection and stability

    Double girder overhead travelling crane in heavy load operation, the main beam will produce a certain degree of deflection, this is a normal structural deformation, but the deflection needs to be controlled within industry standards, generally the maximum deflection of the main beam does not exceed 1/1000 of the span, if the deflection exceeds the standard, it will lead to the lifting equipment shaking, the crane operation stalling, and even affect the service life of the structure.

    When selecting the type, the supplier should be required to provide the deflection calculation report of the main beam to ensure the structural integrity under heavy load; at the same time, the overall stability of the crane needs to meet the requirements, especially in the high-altitude operation, windy environment, the car body without obvious shaking, to ensure the smoothness of the lifting operation.
    Henan Mine crane double girder lifting equipment, the main beam deflection is controlled within industry standards, structural stability, can meet the stability requirements of chemical heavy lifting.

    Step 5 – Match the operating level and operating frequency

    Cranes in chemical plants operate frequently, start and stop frequently, the operating level directly determines the configuration of the core components and the service life of the equipment, if the operating level is selected low, the core components will wear out quickly, resulting in frequent equipment failures. The operating level should be approved according to FEM, ISO or CMAA standards, and the core is to match the actual operating frequency and load status of the plant.

    For double girder overhead travelling crane in chemical plant area, the operation level is generally not lower than FEM A6, and if it is a heavy lifting area for continuous operation, FEM A7/A8 heavy load level should be selected. This type of crane, motor, gear box, brake and other core components are designed according to high-frequency start and stop, motor selection of wire-wound asynchronous motor or inverter motor, with good starting and braking performance, to adapt to frequent forward and reverse operation; gear box selection of hardened gear, strong load-bearing capacity, wear and tear is small, suitable for long-term heavy-duty operation.

    At the same time, need to consider the cooling mode of the motor, high-frequency start-stop motor is easy to generate heat, need to choose the forced air-cooled motor, to ensure that the motor can run normally in a high temperature environment, to avoid overheating and burnt out the motor. The reliability of the brake is the most important, need to choose heavy-duty brake, braking torque is sufficient, can be under heavy load fast, smooth braking, and has good wear resistance, adapt to frequent braking operations. Henan Mine Crane’s chemical double girder equipment is configured according to FEM A7/A8 heavy-duty standards, with motors and brakes adapted to high-frequency starting and stopping needs, which can meet 24-hour continuous operation.

    5-400t double girder crane for chemical equipment hoisting

    5-400t double girder crane for chemical equipment hoisting

    Step 6 – Perfectly configured safety and redundancy system

    The danger of the chemical environment determines that the crane safety system can not have any shortcomings, a single safety protection measures can not cope with the complexity of the operational risks, the need to configure a perfect safety and redundancy system, to achieve ‘multiple protection, layer by layer,’ to eliminate safety accidents from all aspects of the operation of the equipment.

    Dual braking system is the core redundancy configuration, crane lifting mechanism and operating mechanism are required to set up the main, vice two sets of braking system, if the main braking system fails, the vice braking system can be immediately put into use, to avoid serious accidents such as falling lifting equipment, loss of control of the vehicle; overload protection system needs to be real-time monitoring of the lifting load, once it exceeds the rated lifting capacity, it will send out an alarm signal and cut off the lifting circuit immediately to prevent structural damage caused by overloading operation. Once the rated lifting capacity is exceeded, the overload protection system will immediately issue an alarm signal and cut off the lifting circuit to prevent structural damage caused by overloading.

    Emergency stop buttons should be installed at all operating points in the plant, including the crane cab, ground operating station and central control room of the plant, so as to achieve multi-point emergency shutdown in case of emergencies; fire-resistant and flame-retardant cables should be selected, so that even if a fire occurs, the burning of the cables can be slowed down, thus gaining time for evacuation of personnel and shutdown of the equipment. At the same time, the crane needs to be configured with lifting height limit, running stroke limit, big car collision avoidance device, to prevent the crane from over-travelling, collision with other equipment, limit switches are selected explosion-proof type, to ensure that the use of hazardous areas of safety.

    Henan Mine cranes in the safety configuration strictly follow the chemical industry standards, all double girder overhead travelling crane are equipped with double braking system, overload protection, emergency stop button and other safety devices, limit switches use explosion-proof type, some high-end equipment is also equipped with a safety monitoring system, real-time monitoring of the equipment operating status, early warning of potential failures.

    Step 7 – Select the appropriate control and automation programme

    The control mode and automation configuration of the crane need to be determined in conjunction with the hazard level and operational requirements of the chemical plant, the core principle is ‘safety first, easy to operate’, not only to ensure the safety of the operator, but also to enhance the efficiency of the lifting operation, and at the same time can be based on the level of intelligence of the plant, consider the integration with the plant control system.

    Reasonable choice of control mode

    The control mode of chemical plant crane mainly has Pendant button box control, wireless remote control and cab control three kinds, need to choose according to the level of hazardous area. zone 1 high hazardous area, preferred wireless remote control control, the operator can be operated remotely in the safe area, to avoid close contact with the flammable and explosive media; button box control for Zone 2 low hazardous area, the button box should be Choose explosion-proof, waterproof, anti-corrosion type, the protection level is not less than IP67; cab control is applicable to heavy, high-frequency operation of the crane, cab need to do explosion-proof, anti-corrosion, heat insulation design, equipped with a good view and ventilation system, the operator’s working environment needs to meet the safety requirements.

    Configuration of variable frequency drive (VFD)

    Variable frequency drive is an important configuration for cranes. By adjusting the speed of the motor, it realises smooth acceleration and deceleration of the crane, avoids the impact load generated by sudden starting and stopping, reduces the mechanical stress on the crane structure and core components, and prolongs the service life of the equipment. At the same time, the frequency conversion drive can accurately control the running speed of the crane, when lifting heavy equipment can be low-speed operation, to enhance the accuracy of lifting; daily operation can be high-speed operation, to enhance operational efficiency.

    Variable frequency drive system needs to use explosion-proof type, and with the crane motor power matching, to avoid frequency overload, the system also needs to have over-current, over-voltage, overheating protection to ensure stable operation. Henan Mine Crane’s chemical double girder equipment can be configured according to customer demand for explosion-proof frequency conversion drive system, to achieve smooth start-stop and accurate speed regulation, some of the equipment is also equipped with the holding brake logic control, anti-swing function, to further enhance the safety of operation.

    explosion proof overhead crane

    explosion proof overhead crane

    Integration with factory control system

    For chemical parks with a high level of intelligence, the crane control system can be integrated with the plant’s DCS/SCADA system to achieve centralised monitoring and remote scheduling of the crane’s operating status. Crane operating parameters, load data, fault information can be uploaded in real time to the central control room of the plant, the management personnel can grasp the real-time operating status of the equipment, and find out the hidden faults in advance; at the same time, remote start-stop and operation scheduling of cranes can be realised through the central control room to enhance the level of intelligent operations in the plant.

    System integration, need to ensure the compatibility of the communication protocol, and all communication equipment are selected explosion-proof type, to ensure the safety of communication in hazardous areas. Henan Mine Crane’s high-end chemical double girder equipment, support and plant DCS / SCADA system integration, some equipment is also equipped with data monitoring system, the operator can clearly understand the working condition of the equipment through the display screen, intelligent operation and maintenance.

    Step 8 – Advance planning for installation and maintenance

    Chemical plant crane selection, not only to focus on the parameters and design of the equipment itself, but also to do a good job in advance of the installation and long-term maintenance planning. Hazardous areas have strict specifications for the installation of equipment, and long-term maintenance is to ensure the stable operation of equipment, the key to extend the service life, if the installation is not standardised, maintenance is not in place, and then the quality of the equipment is difficult to play a role.

    Crane installation needs to have explosion-proof equipment installation qualification of professional team construction, especially Zone 1 hazardous area installation, all construction steps need to comply with the explosion-proof safety norms, after the completion of the installation needs to carry out explosion-proof testing and test run, to ensure that the equipment’s explosion-proof performance and operational performance to meet the standards, before being officially put into use. During the installation process, the equipment needs to be well protected to avoid chemical media splashing and dust accumulation, affecting the anti-corrosion and explosion-proof effect of the equipment.

    According to the operating level of the crane and the degree of environmental corrosion, a detailed inspection and preventive maintenance programme should be formulated. Regularly inspect the explosion-proof parts, anticorrosion coating, braking system and grounding system of the equipment, and promptly find out the problems such as aging of parts, broken coating, poor grounding, etc. Regularly add anticorrosive and high-temperature-resistant lubricating grease to rotating parts such as gearboxes and bearings, and regularly test the wire ropes, hooks and other easy-to-wear parts, and replace them immediately when they reach the end-of-life standard.

    At the same time, the need to ensure the adequate supply of certified spare parts, explosion-proof, anti-corrosion parts of the crane are special spare parts, the need to use the original factory certified spare parts, to avoid the use of non-standard spare parts lead to equipment explosion-proof, anti-corrosion performance decline, the supplier needs to have a perfect spare parts supply system, can respond to the demand for spare parts in a timely manner, to reduce the downtime of the equipment. Henan Mine cranes have more than 30 service sites covering the whole country, equipped with professional after-sales team, 24-hour rapid response, delivery of conventional parts within 24 hours, but also provide free installation and commissioning services, free replacement of core parts during the warranty period, to provide chemical customers with a full life-cycle maintenance services.

    Chemical plant crane selection of common misconceptions

    In many years of crane selection and service in the chemical industry, found that many companies will be due to the lack of understanding of chemical conditions, the pursuit of cost control, caught in all kinds of selection misunderstandings, ultimately leading to frequent equipment failures, safety accidents hidden, and even face regulatory penalties, these common misunderstandings need to be avoided in advance.

    In order to reduce the initial procurement costs, the choice of non-explosion-proof design of ordinary cranes, this type of equipment in the hazardous areas of operation, it is very easy to produce sparks triggered by explosions, it seems to save the procurement costs, in fact, pay a greater price for safety; underestimation of the degree of exposure to corrosion of the plant, only to do the basic anticorrosion treatment, not according to the standard design of the C4/C5, resulting in serious corrosion of the equipment within a short period of time, and the cost of maintenance and replacement of the later period much higher than the initial investment in corrosion prevention.

    Neglect of local compliance standards, only focus on international certification without obtaining the local explosion-proof certificate, resulting in equipment can not pass the safety acceptance, can not be put into normal use; did not verify the qualifications of the supplier, the selection of suppliers without the qualification of the production of explosion-proof equipment, explosion-proof equipment, anticorrosion design does not meet the standards, there are serious safety hazards; only focus on the selection of equipment, did not plan for the long-term maintenance plan, the maintenance of the late in place, resulting in rapid aging of the equipment, the service life of a substantial amount of money. This leads to rapid aging of the equipment and shortens its service life.

    Many chemical companies have used the equipment of unqualified suppliers, explosion-proof performance does not meet the standards, anti-corrosion coating off and other issues, while the customers who choose Henan Mine cranes, because the enterprise has a perfect qualification, mature chemical cases and professional after-sales team, effectively avoiding these selection mistakes, equipment operation stability has increased dramatically.

    Case example: Henan Mine Crane double girder explosion-proof overhead travelling crane chemical application cases

    Henan Mine cranes plough into the chemical industry for many years, undertake a number of large-scale chemical and petrochemical projects, has accumulated a wealth of experience in customisation, the following two typical cases are shared for your reference, a more intuitive understanding of the chemical conditions of the double girder overhead travelling crane selection and application results.

    Case 1: 300t double girder overhead travelling crane project for a high-end chemical equipment manufacturer in Shandong province.

    The enterprise is mainly engaged in high-end chemical equipment manufacturing, need to lift large chemical reactors, heat exchangers and other equipment, the operating area for the ATEX Zone 2 explosive gas environment, the presence of a small amount of organic solvent vapour, the environment of the medium degree of corrosion, the requirements of the crane has a heavy-duty lifting capacity and explosion-proof, corrosion-resistant, and can be adapted to high-frequency start-stop operations.

    Combined with the needs of the enterprise, Henan Mine Crane customised a 300-tonne double girder explosion-proof overhead travelling crane, with a span of 30m, a lifting height of 22m, and an operating level of FEM A8, which is fully adapted to the needs of heavy-duty and high-frequency operations; the explosion-proof design is carried out according to the ATEX II 2G standard, and all the electrical components are selected to be of the explosion-proof type, with a perfect anti-static grounding system, and ATEX certification and domestic explosion-proof certificates. Anti-corrosion treatment is carried out according to C4 standard, the main beam adopts three-layer protection of sandblasting rust removal + epoxy zinc-rich paint + fluorocarbon paint, 316 stainless steel is used for fasteners, and the trolley adopts a fully enclosed sealing design, which can effectively block the intrusion of medium and dust.

    At the same time, the equipment is equipped with explosion-proof variable frequency drive system, to achieve smooth acceleration and deceleration, reduce mechanical stress, but also configured with PLC + frequency converter communication control, the use of digital filtering technology of the frequency converter, improve the crane’s operating accuracy; cab adopts rotary integrated operation linkage table, with safety monitoring system, data monitoring system, the operator through the display screen can clearly understand the working condition of the crane.

    Since the commissioning of the equipment, it has smoothly completed the lifting operation of 300-tonne heavy chemical equipment, high-frequency starting and stopping trouble-free operation, explosion-proof and anti-corrosion performance is fully adapted to the working conditions of the plant, high lifting accuracy, there is no equipment collision, media corrosion, and other issues, which effectively enhance the production efficiency of the enterprise, and has been highly recognized by the customer. The project is also Henan Mine Crane manufactured in the field of high-end chemical equipment, an important breakthrough, highlighting the technical strength of enterprises in the field of large-tonnage chemical cranes.

    Case 2: a semiconductor materials chemical enterprise clean explosion-proof double girder overhead travelling crane project

    The semiconductor materials chemical enterprise’s production workshop, air cleanliness level 4, while the presence of flammable and explosive gases, explosion-proof grade requirements to dIICT4, the need for cranes with clean, explosion-proof, automation features, to avoid dust contamination, and at the same time, can achieve accurate lifting and automatic operation.

    The equipment adopts automatic computer control in the central control room, which can automatically run the reduction furnace and silicon rod tools from the reduction furnace platform, cleaning platform, transit platform and other locations, according to the set working route, and at the same time, it has a manual operation mode, and the interlocking between the remote control and the handle control ensures the safety of the operation; the large and small car running mechanism adopts laser bar code positioning, which is accurate and avoids any deviation.

    After being put into operation, the equipment fully meets the clean and explosion-proof requirements of the semiconductor materials chemical workshop, with smooth automatic operation, no dust pollution and high lifting accuracy, which effectively adapts to the special production process of the enterprise and provides reliable support for the continuous production of the enterprise.

    Chemical plant double girder overhead travelling crane procurement checklist

    In order to avoid omitting key requirements when selecting double girder overhead travelling crane, we have compiled a purchasing checklist based on the operating characteristics of chemical industry, which can be checked one by one according to the actual situation of the plant to ensure the accuracy and compliance of the selection:

    1. has completed the plant hazardous area classification (Zone 1/Zone 2), clear gas / dust explosion-proof type

    2. the required explosion protection certificates (ATEX/IECEx/local certificates of conformity, etc.) for the equipment have been determined

    3. the actual lifting load has been accurately verified, a reasonable safety margin has been reserved, and the rated lifting capacity has been specified.

    4. the crane span has been approved in combination with the column distance of the plant, and the load-bearing capacity of the travelling beam of the plant has been verified.

    5. the level of corrosion protection (C4/C5) has been specified according to the degree of corrosion, clear material selection requirements

    6. has been combined with the frequency of operation to determine the level of operation (FEM / ISO / CMAA)

    7. has specified the control mode (button box / remote control / cab), to determine the automation and system integration requirements

    8. has confirmed that the supplier has explosion-proof equipment production qualification and professional installation team (such as Henan Mine Crane, with a complete production, installation, after-sales qualification)

    9. has a clear spare parts supply system and maintenance plan

    10. have verified that the overall design of the equipment meets the local chemical industry safety standards

    Frequently Asked Questions

    Henan Mine Crane  Professional Clean Energy Base Explosion-Proof Crane

    Why must chemical plants use explosion-proof overhead travelling cranes?

    In chemical plants, flammable and explosive gases, vapours or dusts are present in the production and storage areas. The electrical parts and mechanical friction parts of ordinary overhead travelling cranes are prone to sparks, which can ignite gases or dusts and lead to explosions. Explosion-proof overhead travelling crane is designed to eliminate the generation and accumulation of sparks, and can operate safely in hazardous environments, which is a necessary safety requirement for chemical plant areas.

    What core certifications are required for cranes in chemical hazardous areas?

    International common core certification for ATEX (EU) and IECEx (International Electrotechnical Commission), need to be selected according to the use of equipment in the region; also need to obtain the local explosion-proof safety certification, such as domestic enterprises need to obtain the National Explosion-proof Inspection Agency issued by the Explosion-proof Certificate of Conformity, all the certificates need to cover the overall equipment of the crane, rather than a single component. Henan Mine Crane’s chemical crane products, are equipped with ATEX, IECEx, CE and other international certifications and relevant domestic qualifications to meet the compliance requirements of different regions.

    Can ordinary double girder overhead travelling crane be modified to fit the chemical environment?

    Retrofitting is not recommended. Ordinary crane infrastructure, electrical components are not designed according to explosion-proof, anti-corrosion standards, the later transformation is difficult to do the whole process of explosion-proof and anti-corrosion protection, after the transformation of the equipment is prone to explosion-proof performance does not meet the standards, anti-corrosion coating falling off and other problems, there are serious safety hazards, and after the transformation of the equipment can not get the formal explosion-proof certification, can not pass the safety acceptance of the plant. It is recommended to directly use Henan Mine Crane and other professional manufacturers of chemical double girder overhead travelling crane, adaptability and safety is more secure.

    How long is the service life of explosion-proof double girder overhead travelling crane in chemical plant?

    Under the premise of good anti-corrosion protection and regular maintenance, the normal service life of explosion-proof double girder overhead travelling crane is 15-20 years; if it is a strong corrosion, high-risk chemical industry, as long as it is designed in accordance with the C5 anti-corrosion standard and the maintenance plan is strictly enforced, the service life can also reach more than 10 years. The service life of the equipment mainly depends on the level of anticorrosion protection and the quality of late maintenance. Henan Mine Crane’s chemical cranes, in the case of standardised maintenance, the average service life of up to 15 years or more, a number of early project equipment has been running stably for more than 10 years.

    Is it necessary to choose double girder structure for cranes in chemical plants?

    Not absolutely. Double girder overhead travelling crane is mainly suitable for heavy equipment lifting, multi-layer layout, high-frequency operation of the chemical plant; for small chemical plant, only lifting light equipment (below 5 tonnes), and low frequency of operation, you can choose explosion-proof and anti-corrosion single girder overhead travelling crane, but need to ensure that the explosion-proof and corrosion-resistant design in line with the requirements of the plant conditions, the level of operation to match the actual demand. Henan Mine Crane can flexibly provide double girder and single girder chemical special cranes according to the lifting requirements and working conditions of customers to meet the needs of chemical enterprises of different sizes.

    Conclusion

    Chemical plant double girder overhead travelling crane selection, always put safety and compliance in the first place, which is the bottom line requirements of chemical production, while the suitability of the equipment is the key to ensure production efficiency. Double girder overhead travelling crane, with its high loading capacity, good stability and flexible lifting height, can be perfectly adapted to the needs of heavy lifting and complex working conditions in chemical factories, while the perfect explosion-proof and anti-corrosion design allows the equipment to operate safely and stably in dangerous and corrosive chemical environments.

    Accurate selection is not a simple parameter matching, but from the environmental assessment, explosion-proof and anti-corrosion design, parameter approval, to the installation and maintenance of the whole process of consideration, any one of the links of negligence, may lead to safety accidents or increase the cost of the later. Only according to the actual working conditions of the plant, the development of customised crane solutions, in order to fundamentally avoid operational risks, eliminate regulatory penalties, so that cranes really become a reliable support for chemical production.

    In the field of chemical cranes, Henan Mine Crane has become the preferred partner of many chemical companies with years of technical accumulation, perfect customisation capabilities and a wealth of industry cases. As a national high-tech enterprises, manufacturing single champion enterprises, Henan Mine Crane has a professional R & D team and automated production lines, according to different chemical conditions, customised to fit the explosion-proof, anti-corrosion double girder overhead travelling crane, from the preliminary conditions of the survey, programme design, to the latter part of the installation, commissioning, maintenance and after-sales service, to provide a full range of services, to help chemical enterprises to achieve safe, stable and efficient production.

    Submit your chemical plant hazardous area classification report, our professional technical team, for your professional working condition assessment;
    According to your lifting needs and environmental characteristics, we will customise an exclusive explosion-proof and anti-corrosion double girder overhead travelling crane scheme to fit your actual operational needs;

    Henan Mine CraneDiscuss your requirements ↗
  • How to Calculate the Total Cost of Ownership (TCO) for a Factory Crane?

    How to Calculate the Total Cost of Ownership (TCO) for a Factory Crane?

    How to Calculate the Total Cost of Ownership (TCO) for a Factory Crane?

    When most factories purchase bridge, gantry, and cantilever cranes, they generally fall into the selection misunderstanding of “only looking at the purchase reserve price”.The service life of the crane can reach 10-30 years, and the initial procurement cost accounts for only 10%-20% of the total cost of ownership. Long–term hidden costs such as energy consumption, operation and maintenance, and downtime are the main expenses.

    TCO whole life cycle cost accounting is the key to optimizing crane investment and improving ROI.This article will explain in detail the definition, cost composition, step-by-step calculation method, influencing factors and cost-reduction strategies of factory crane TCO, so as to help enterprises abandon one-sided price comparison thinking and realize the optimal cost of the whole life cycle of equipment.

    What Is Total Cost of Ownership (TCO) for a Factory Crane?

    The TCO (Total Cost of ownership) of a factory crane refers to the sum of all direct and indirect costs in the whole life cycle of the crane from procurement and commissioning, daily operation, maintenance and overhaul, to final scrap disposal, covering the complete service cycle of the equipment for 10-30 years. The specific life span depends on the working conditions of the equipment, maintenance quality and design standards.

    Unlike a single purchase price, TCO accounting completely breaks the one-sided thinking of “only looking at the initial investment”, and comprehensively includes hidden expenses that can easily be ignored such as energy consumption, labor, downtime, and compliance rectification.

    Accurate TCO analysis can help companies scientifically compare the cost performance of cranes of different brands and configurations, and rationally adopt high-priced, high-quality, energy-saving and efficient equipment solutions to reduce the whole life cycle cost from the root cause and improve the economic efficiency of equipment operations.

    Core Composition and General Calculation Formula of the TCO of Factory Crane

    The industry’s general crane TCO accounting formula integrates all income and expenditure items in the whole life cycle and is a standardized accounting basis:

    TCO = initial acquisition cost + operating cost + maintenance and repair cost + downtime capacity loss + safety compliance cost + scrap disposal cost−equipment residual value

    The proportion of each cost module is a common estimate in the industry, and it will fluctuate slightly with the crane tonnage, working condition intensity, use environment, and regional policies. The specific breakdown is as follows:

    Initial acquisition cost

    It is a one-time initial investment and is the most intuitive cost item. It includes all pre-production expenditures such as equipment procurement, transportation, installation, infrastructure transformation, qualification approval, acceptance testing, and initial personnel training. It is also the core reference item for market price comparison.

    Operating costs

    The cost module with the highest proportion of the whole life cycle is the core of long-term expenditure. It mainly includes equipment energy consumption, operator salaries, equipment insurance, and replacement of consumables. Among them, power consumption and labor costs account for the absolute dominance of operating costs.

    Maintenance and repair costs

    It covers daily preventive maintenance, regular compliance testing, replacement of wearing parts, emergency repair of faults, annual maintenance contracts and other expenses.The longer the service life of the equipment and the harsher the working conditions, the higher the maintenance cost, and unplanned maintenance of sudden failures will significantly increase additional expenses.

    Loss of downtime capacity

    The hidden costs that are most easily overlooked but have a great impact include planned maintenance shutdowns, production capacity stagnation caused by sudden failures and shutdowns, labor inactivity, order delays, and expedited production premiums. The loss of downtime in high-capacity assembly line factories far exceeds equipment maintenance expenses.

    Safety compliance cost

    Expenditures incurred to meet OSHA, ASME, CMAA and other industry standards and local regulatory requirements, including personnel certification training, safety equipment upgrades, compliance audits, annual inspections and records, emergency response to accidents, etc., Non-compliance will also result in high fines, further driving up costs.

    Scrap disposal cost and equipment residual value

    This item covers the finishing costs of disassembly, clearance and environmental protection disposal of the crane after the expiration of its service. At the same time, the remaining residual value of the equipment can offset the overall input. It is an indispensable last part of the TCO’s full-cycle accounting, which directly affects the final net input cost of the equipment.

    Step 1 — Calculate the Initial Investment Cost of a Factory Crane

    The initial investment is all fixed expenditures before the crane is put into operation. The core formula: initial total investment = equipment purchase price + transportation fee + installation and commissioning fee + infrastructure renovation fee + approval and testing fee + initial training fee + emergency reserve fund (5%-15%)

    Breakdown of costs and case accounting:

    • Equipment purchase price: including core equipment such as hoists, carts, and electronic control systems, the standard model of a 50–ton double–girder bridge crane is US1180,000, and the configuration of variable frequency drive (VFD) and wireless remote control requires an additional premium of 10%-25%; the market price of a 5-10–ton single-girder crane is US330,000-80,000, and customized models for large tonnage, explosion-proof, and clean rooms can reach more than US4400,000-1000,000.
    • Transportation and distribution costs: The industry routinely accounts for 5%-15% of the equipment purchase price. In this case, the accounting cost is US115,000. The specific cost fluctuates flexibly with the transportation distance, the tonnage weight of the equipment, and the mode of transportation (land/sea/railway).
    • Installation and commissioning fee: it accounts for 15%-40% of the equipment purchase price, and the installation cost of indoor standard working conditions is US660,000; for special working conditions such as aerial work and outdoor complex scenes, the installation cost can reach more than US。100,000.
    • Infrastructure renovation fee: it covers supporting projects such as crane track laying, foundation reinforcement, plant steel structure renovation, and circuit system upgrade.The cost of retrofitting the old plant will even exceed the equipment procurement itself. In this case, the cost of retrofitting is US995,000. The selection of compact low-clearance cranes can effectively reduce the cost of infrastructure retrofitting.
    • Approval and testing fees: including project compliance reporting, structural load accounting, third-party load testing, equipment acceptance and filing and other compliance expenses, the total in this case is US113,000 (approval fee of US88,000 + testing fee of US55,000).
    • Initial personnel training: it covers the pre-job compliance practical training of crane operators, engineers, and maintenance technicians. The training cost in this case is US44,000 to ensure that the equipment can be put into operation to standardize compliance operations.
    • Emergency reserve fund: It is calculated at 10% of the overall initial investment and is used to cover unknown expenditures such as construction renovation changes, formalities additions, and sudden supporting rectification. In this case, the reserve fund totaled US336,700 to avoid the risk of budget overruns in the early stage.

    Total initial investment in the case: US4403,700

    Step 2 — Estimate Factory Crane Operating Costs

    Operating cost is the annual fixed + floating expenditure during the service period of the equipment, and the cumulative expenditure in 20 years far exceeds the initial investment. The core formula: Annual operating cost = energy consumption + labor salary + equipment insurance + consumables expenses + other miscellaneous expenses

    Accounting details based on case equipment (annual operation of 2,500 hours, medium working conditions, mid-West plant in the United States):

    • Energy consumption: The average operating power of the equipment in this case is 25kW, which is calculated based on the US industrial electricity price of 0.12 US dollars/kWh and the annual working conditions of 2,500 hours, and the annual electricity consumption is 7,500 US dollars.Energy-saving cranes equipped with VFD frequency conversion control and regenerative braking system can effectively reduce power loss by 20%-50%, and have significant long-term energy-saving benefits.
    • Labor cost: The equipment is equipped with 1.5 full-time operators, covering all labor expenses such as basic salary, employee benefits, and overtime subsidies. The total annual labor cost is US997,500, which is the core expenditure of the crane’s annual operating cost.
    • Equipment insurance: it includes crane-specific property insurance, third-party liability insurance and other necessary insurance types to avoid economic risks caused by equipment damage and operating accidents. The annual insurance premium is US44,000.
    • Miscellaneous consumables: it covers daily consumables such as equipment grease, wireless remote control batteries, cleaning and maintenance consumables, and the annual comprehensive consumables cost is US11,500.
    • Other expenses: including miscellaneous expenses such as supporting energy consumption in the work area, equipment intelligent monitoring system subscription, auxiliary operation and maintenance consumables, the total annual expenses are US11,000

    Step 3 — Include Maintenance and Repair Expenses

    The maintenance cost includes planned maintenance and sudden failure maintenance. After 5 years of use of the equipment, the wear and tear will intensify, and the maintenance cost will increase year by year. The core formula: Annual maintenance cost = preventive maintenance cost + compliance annual inspection fee + parts repair and replacement fee + emergency reserve fund

    Case accounting details:

    • Preventive maintenance: It includes standardized maintenance work such as regular lubrication and maintenance of equipment, commissioning and calibration of key components, and inspection of normalized equipment to reduce equipment wear and potential failures from the source. The annual maintenance cost is US33,500.
    • Annual compliance inspection: strictly follow OSHA and ASME industry specifications, carry out annual comprehensive inspection of the whole machine, load performance testing and compliance ledger filing to ensure the legal and compliance operation of the equipment, and the annual inspection and compliance fee is US33,000.
    • Repair and replacement of accessories: it covers the regular replacement of core wearing parts such as wire ropes, braking devices, and limit switches, as well as the daily minor troubleshooting and maintenance of equipment. Based on years of working condition data, the average annual expenditure is US44,500.
    • Emergency reserve fund: Used to deal with unexpected expenses such as sudden equipment failures and emergency overhauls. It is calculated at 10% of the total annual fixed maintenance cost, and the annual reserve amount is US11,100, which effectively avoids the risk of sudden cost overruns.

    Step 4 — Calculate Downtime and Productivity Losses

    Downtime loss is the most easily overlooked high cost. It is divided into planned maintenance downtime and sudden failure downtime, which directly affect factory production capacity and order revenue. The core formula: Annual downtime loss = (Planned downtime time + unplanned downtime time) × (Unit hour capacity loss + unit hour labor idle cost) × Capacity utilization rate + sudden accident premium loss

    Case accounting parameters: the hourly production capacity loss of the factory area is US11,200, the labor idle cost is US880/hour, the capacity utilization rate is 80%, the annual planned shutdown is 12 hours, the unplanned shutdown is 20 hours, and the annual emergency amortization reserve is US55,000.

    Total annual downtime losses in the case: US337,768, a total of US7755,000 in 20 years (in continuous production plants, the hourly production capacity loss can reach US55,000–20,000, and the downtime loss will become the largest proportion of TCO)

    Step 5 — Consider Crane Safety and Compliance Costs

    Compliance cost is the basis for the legal and safe operation of equipment, which can effectively avoid high fines and safety accident losses. The core formula: Annual compliance cost = personnel certification training + safety equipment upgrade + compliance audit filing + protective consumables + accident emergency reserve fund

    Case accounting details: annual personnel retraining is US33,500, safety equipment upgrade and replacement is US22,000, compliance audit and ledger management is US11,500, protective equipment and identification are US8800, and the reserve for accidents and policy adjustments is US22,000.

    Total annual safety compliance cost of the case: US99,800, cumulative US1196,000 in 20 years

    Step 6 — Evaluate Crane Lifespan and Residual Value

    Equipment service life, maintenance status, and market conditions directly determine the residual value, and the final accounting is completed based on the full cycle data. The core formula: net residual value = second-hand residual value of equipment−scrap disposal cost, final TCO = initial total investment + annual cumulative long-term cost−net residual value

    Case accounting parameters: equipment design and service life of 25 years, medium working conditions, complete maintenance records, second-hand residual value of 12% of the original purchase price (US221,600), equipment disassembly, clearance, environmental protection disposal costs of US112,000, net residual value of US99,600.

    Long-term cumulative cost of the whole cycle (20 years):(111500+12100+37768+9800)×25 = US 44,279,200

    The final 25-year full life cycle TCO:403700 + 4279200 − 9600 = 4673,300 US dollars, the average annual TCO is about 186,932 US dollars

    Core Key Factors Affecting the Crane TCO

    The TCO of the whole life cycle of the crane is not a fixed value, and it will fluctuate dynamically with the equipment usage conditions and management methods.To accurately control costs and scientifically optimize investment benefits, enterprises need to accurately grasp the core influencing factors, and systematically optimize from the dimensions of equipment selection, on-site working conditions, operation and maintenance management, and supply chain services.

    Equipment operating conditions and load utilization rate

    The higher the frequency of equipment hoisting, the greater the rated load, and the longer the continuous operation time, the faster the wear rate of mechanical structure and transmission components, which directly pushes up the comprehensive costs of energy consumption, maintenance and downtime losses.Enterprises need to strictly select models based on CMAA and FEM international working conditions, match the real production load, eliminate the mismatch of “small machine overload, large machine low load”, and control invalid losses from the source.

    On-site operating environment conditions

    Harsh working conditions such as dust, acid-base corrosion, high temperature exposure, and outdoor humidity will accelerate the aging and failure of core components such as wire ropes, braking systems, and main beam steel structures.Such scenarios require special models with anti-corrosion, dust-proof, and high temperature resistance, and at the same time need to encrypt the maintenance frequency. Compared with standard indoor working conditions, the overall TCO can be increased by 30%-100%, which is an important cost variable that cannot be ignored.

    Design specifications and accessories versatility

    A modern crane equipped with VFD frequency conversion speed regulation, lightweight main beam structure, and general standardized accessories has the advantages of low energy consumption, low failure rate, easy purchase of accessories, and convenient maintenance, which can sustainably compress long-term operating costs.On the other hand, niche customized models and non-standard design equipment generally have problems such as scarcity of accessories, high maintenance thresholds, and serious maintenance premiums, and the TCO of the whole life cycle will be significantly higher.

    Maintenance management system and operation and maintenance strategy

    A scientific predictive and preventive maintenance system can effectively reduce unplanned downtime by 50%-80%, and greatly improve equipment attendance.The traditional passive operation and maintenance mode of ”emergency repair after failure” can easily cause problems such as sudden major repairs and long-term shutdowns, which continue to increase equipment maintenance costs and production capacity losses, which are the core management incentives for the high TCO.

    Brand after-sales and supporting service system

    The layout of the supplier’s local service outlets, the inventory of standing parts, and the timeliness of emergency response directly determine the length of equipment failure and downtime and maintenance costs.A perfect localized after-sales support system can quickly deal with equipment failures, shorten the shutdown cycle, and reduce hidden losses in operation and maintenance. It is a key external factor in controlling the long-term TCO of the crane.

    Factors That Can Reduce Factory Crane TCO

    Based on the TCO cost structure, priority is given to optimizing the high proportion of operation, downtime, and maintenance costs, which can achieve significant cost reduction throughout the life cycle.:

    • Scientific selection and rejection of low-price traps: match tonnage and working condition levels as needed, and do not blindly match high and low; give priority to low-headroom, lightweight, and energy-saving models to reduce infrastructure transformation and long-term energy consumption costs; optimize standardized accessory models to reduce follow-up maintenance premiums.
    • Equipped with energy-saving intelligent configuration: the installation of VFD frequency conversion drive, regenerative braking, and intelligent load monitoring system can reduce power consumption by 20%-50%; the operating status of the equipment is monitored in real time through IoT devices to achieve early warning of failures and avoid sudden shutdowns.
    • Implementation of standardized preventive maintenance: establish an electronic maintenance ledger for equipment, carry out regular inspections, lubrication, and replacement of accessories; sign a long-term maintenance contract with a manufacturer, lock in low-cost maintenance resources, enjoy priority after-sales response, and greatly reduce the probability of failure.
    • Strengthen personnel compliance training: regularly carry out certification retraining of operators and maintenance personnel, standardize operating procedures, reduce equipment damage and safety accidents caused by human operation errors, and reduce compliance fines and maintenance costs.
    • Optimize one-stop delivery suppliers: choose suppliers that can provide one-stop procurement, installation, training, and lifetime after-sales service to avoid coordinated costs and hidden price increases caused by multi-party docking, and ensure the stable operation of the equipment throughout the cycle.

    Conclusion

    Many factory cranes have a service life of more than 20 years. Under this premise, the initial purchase price of equipment is no longer the key to the selection decision, and it only accounts for a very low proportion of the total cost of the whole life cycle.To judge the investment value of a set of lifting equipment, the core lies in the comprehensive control ability of long-term energy consumption, maintenance, shutdown and shutdown losses, and compliance-related costs.

    Relying on a perfect intelligent manufacturing system and advanced energy-saving technology, Henan mine crane meet the requirements of cost reduction in the whole life cycle of factory equipment, and solve common problems in the industry in a targeted manner: high energy consumption of equipment, frequent failures, complex maintenance processes, large losses caused by downtime, etc., and continuously optimize the total cost of ownership (TCO) of equipment.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Calculate the Span of an Overhead Crane?

    How to Calculate the Span of an Overhead Crane?

    How to Calculate the Span of an Overhead Crane?

    Doing crane sales and technical support for many years, the most common question asked by customers is “what span of overhead crane should be selected for the workshop”. Many people mistakenly think that they only need to measure the width of the workshop, but in fact, the span is the core parameter of overhead crane design, and miscalculation will affect the installation, safety, wheel pressure distribution and equipment life. In this article, we will explain the definition of span, calculation methods, factors and common misunderstandings, to help you avoid the pit.
    overhead crane

    What is the span of an overhead crane?

    The basic definition of crane span

    Crane span is not the width of the workshop or the edge of the track distance, but the horizontal distance between the centerline of the two crane tracks. For example, when the width of the track is 100mm and the distance between the outer edges is 22.7 meters, it is wrong to directly take 22.7 meters as the span, the correct practice is to find the midpoint of the width of the two tracks and measure the distance between the midpoints, single girder and double girder overhead cranes are applicable to this standard.

    Why span is crucial in crane design

    Span directly determines the selection of crane structure: small span can be used single girder overhead crane (single girder overhead crane), large span needs double girder overhead crane (double girder overhead crane), otherwise the main girder is easy to deformation. It also affects the wheel pressure and end beam design, the larger the span, the more uneven distribution of wheel pressure, end beams need to be more robust; at the same time associated with the workshop layout, hook coverage, as well as manufacturing costs and equipment stability, and need to comply with the GB/T 14405-2011 standard span series requirements.

    The standard meaning of span in different crane types

    Overhead crane span

    The span of overhead bridge crane is the distance between the centerlines of two runway tracks on the steel beams of the workshop, and the measurement should be based on the centerline of the tracks on the runway beams, not the edge of the steel beams.

    Gantry crane span

    The span of gantry crane (gantry crane) is the distance between the centerline of two runway tracks on the ground, mostly used in open field, the measurement needs to be carried out in windless horizontal conditions to avoid thermal expansion and contraction errors, and its span is usually 18-40 meters, graded in 5-meter intervals (GB/T 14406-2021 standard).

    The span difference between single girder and double girder crane

    The span definition of single girder and double girder overhead crane is the same, but the structural arrangement and gap requirements are different: double girder cranes need to reserve more safety gaps, and single girder cranes gap requirements are relatively loose, but they all need to comply with safety standards.

    How to calculate the span of overhead crane

    Core formula

    Crane span = distance between two runway track centerlines, no need for complex calculations, the key is to find the right centerline, measure the distance.

    Step 1: Find the centerline of the runway tracks

    Can measure the width of a single track and take the midpoint mark, if the track has been installed, the laser range finder can be aligned with the midpoint of the inside of the track, Henan Mine Crane engineers commonly used in home surveys this method, accurate and efficient.

    Step 2: Measure the distance between the centerlines of two tracks.

    Need to use qualified tape measure or laser rangefinder on-site measurement, can not directly use the theoretical value of the drawings (old workshop track is easy to offset, wear and tear); measurement of the tape measure needs to be naturally sagging, large spans need to be measured more than a few points to take the average value.

    Step 3: Confirm the tolerance and design standard

    According to ISO and GB/T 14405-2011 standards, the tolerance is allowed to be ±3mm when the span is ≤10 meters, and the larger the span is, the larger the tolerance range is, but not more than ±5mm; at the same time, it needs to be combined with the manufacturer’s design requirements, and Henan Mine Crane will adjust the dimensions of the main girder and end girder according to the actual measured span and the tolerance to guarantee the stability of the operation.

    Calculation example

    If the distance from the center line of the left rail to the center line of the right rail measured on site is 22.5 meters, the crane span is 22.5 meters. This value directly determines the main girder, end girder design and wheel pressure accounting, which is the core basis of the quotation and design program, and miscalculation will lead to rework and additional costs.
    overhead crane

    The difference between building width and crane span

    Why the building width can not be directly equal to the crane span

    Workshop columns, track beam supports, pedestrian access and track beam offset will narrow the distance from the centerline of the track, and the two cannot be equated. According to GBJ6 “plant building modulus coordination standard”, crane span S = plant span L – b (b is the difference between the two, determined by the presence or absence of access).

    Example comparison

    A workshop building width of 24 meters, the measured distance from the centerline of the track is only 22.5 meters, due to the two sides of the columns need to reserve a safety gap and track beam offset. If the span is set at 24 meters, the crane will not be able to be installed and will need to be re-customized.

    Key factors affecting the span selection of overhead cranes

    Workshop or steel structure layout

    Column spacing determines the upper limit of the span (track beams need to be fixed to the columns), and the runway beam layout also affects the distance from the centerline of the track; the existing building needs to be combined with the steel structure limitations to determine the span according to the existing track.

    Lifting Coverage Requirements

    The span needs to meet the hook to cover all the operation areas (material area, production line, etc.), to avoid affecting the production efficiency due to insufficient span.

    Crane type and tonnage

    Light load cranes (5 tons, 10 tons) span can be slightly larger, heavy load cranes (50 tons, 100 tons) span should not be too large, otherwise the strength of the main beam is insufficient; different tonnage cranes have a standard span series (GB/T 14405-2011), Henan Mine Crane will be recommended according to the need.

    Safety clearance requirements

    The clearance between the crane and the column and wall should be not less than 100mm and 50mm respectively, and at the same time, the space for maintenance and installation should be reserved to facilitate component maintenance.

    Future expansion considerations

    The span can be reserved for a small amount of margin, to adapt to the workshop’s future expansion needs, to avoid the later replacement of the crane to increase costs.

    How the span affects the cost and performance of the crane

    The larger the span, the more steel structure is required.

    The larger the span, the longer the main beam, the larger the cross-section size, the increase in steel consumption (every 5 meters increase in span, the average increase in steel consumption of the main beam by 15%), and the need for high-strength steel, manufacturing costs rise.

    Impact on wheel pressure and track system

    The larger the span, the more uneven the wheel pressure, the need to reinforce the track beams, replacement of wear-resistant wheelsets, otherwise easy to lead to track deformation, fracture, and increase maintenance costs.

    Balance between coverage and economy

    The span only needs to meet the coverage requirements, too large will only increase costs and reduce stability, Henan Mine Crane engineers will help customers measure the optimal span, to achieve a balance between economy and practicality.
    overhead crane

    Common mistakes when calculating crane span

    Confusing the distance between the outer edge of the track and the centerline of the track

    Directly measure the distance of the outer edge of the rail as the span, ignoring the thickness of the rail, which will easily lead to a large span, the crane can not be installed.

    Replacing track spacing with building width

    Neglecting the space occupied by the workshop structure and setting the span according to the building width will lead to the crane not being able to adapt to the site and increase the rework cost.

    Neglecting installation tolerances

    Track installation deviations (e.g. non-parallel) exceeding the allowable range will lead to crane runout, jamming, and damage to the wheelset and track.

    Failure to check hook coverage and side approach distance

    Accounting for spans only and ignoring hook coverage and side approach distances can result in the inability to lift materials in a specific area, affecting production.

    Assuming that all crane suppliers have the same reference dimensions

    Different manufacturers crane structure design is different, span reference size is different, according to other manufacturers size accounting, easy to size mismatch.

    What information should you provide to crane suppliers?

    Necessary dimensions

    It is necessary to provide the measured distance from the centerline of the track, lifting height, crane tonnage, actual dimensions of the workshop and detailed parameters of the runway beam to provide a basis for the design.

    Useful supporting documents

    Workshop CAD drawings, site photos, existing runway dimensions and production handling requirements can help the supplier to accurately give span recommendations and optimize the configuration.

    Example of workshop overhead crane span calculation

    The workshop of a machinery processing factory is 25m wide, with 23m spacing between columns, lifting 5 tons of mechanical parts, which needs to cover the whole workshop and reserve space for maintenance. Henan Mine Crane engineers measured the centerline distance of the track 22.5 meters, and finally determined the span, which not only meets the installation requirements, meets the demand for coverage, but also adapts to the single girder crane, saving costs and stable operation.
    overhead crane

    Frequently asked questions about overhead crane spans

    Is crane span the same as crane width?

    No, they are not. Span is the distance from the centerline of the track, the width is the size of the equipment itself, such as Henan Mine Crane 22.5 m span single girder crane, its own width is only about 2.5 meters.

    Can only rely on architectural drawings to calculate the span?

    No. The drawings are theoretical values. Drawings for the theoretical value, the site track may be offset, need to measure the centerline distance of the track to be accurate.

    What if the workshop has already been built?

    If the track has been installed, the centerline distance will be measured; if not installed, we can contact Henan Mine Crane engineers to come to the workshop to determine the location and span of the track.

    Does the span have a big influence on the price?

    The impact is large, every 1 meter increase in span, the cost increases, the span of more than 30 meters after the increase is more pronounced, the same tonnage of 20 meters and 25 meters span crane price difference of about 10% -15%.

    Is the final span confirmed by the buyer or the manufacturer?

    Both sides to confirm: the buyer to provide site and demand information, manufacturers combined with standards and experience to give advice to avoid mistakes.

    Conclusion

    The core of calculating the span of overhead crane is to measure the distance between the centerlines of two rails, and determine it by combining the tolerance, workshop layout and production demand. Do not calculate by feeling or building width, ignoring the actual measurement and tolerance will cause problems.

    Henan Mine Crane has rich experience in survey and design, and can help customers accurately calculate the span.

    Need to confirm the span of your overhead crane? Send us your workshop drawings, track dimensions or on-site photos, Henan Mine Crane engineering team will check the span, lifting height and configuration free of charge, and provide you with professional advice within 24 hours to help you avoid pitfalls and save money.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Calculate the Right Crane Capacity for Your Project

    How to Calculate the Right Crane Capacity for Your Project

    How to Calculate the Right Crane Capacity for Your Project

    In engineering scenarios such as construction, factory operation and maintenance, port loading and unloading, and steel metallurgy, the reasonable selection of the rated capacity of the crane directly affects construction safety, operating efficiency and project cost.Most safety accidents, construction delays and equipment losses are rooted in the fact that the early capacity calculations are based on experience alone, ignoring key factors such as the weight of the spreader, dynamic load and operating environment, resulting in equipment that is either idle and wasteful of investment or overloaded for a long time. Operation.Accurate calculation of lifting weight is a prerequisite to ensure the safe operation of the crane and take into account the economy.

    What Factors Determine the Required Crane Capacity?

    The rated load required for Henan Mine Crane manufactured cranes is not determined by the weight of a single heavy object, but is the result of a comprehensive determination of the parameters of the whole operation scene and the whole process.The omission of any parameter will lead to a deviation in the capacity calculation, laying safety and cost hidden dangers for the project.The following six core factors are the basic basis for all crane load calculations, covering static, dynamic, environmental and long-term use needs.

    Load weight

    The self-weight of the load is the core benchmark for the calculation of crane capacity, which refers to the net weight of the core heavy object in a single hoisting operation, and it is also the primary reference data for selection.It should be noted that the load weight here is by no means a rough valuation, and must be based on the precise net weight marked on the equipment drawings, material parameter sheets, and cargo nameplates.In actual projects, many materials will be accompanied by ancillary accessories, such as connecting brackets for steel structure components, fixed bases for equipment, packaging reinforcement parts for goods, etc. Such ancillary weights must all be included in the total load, and the main body weight cannot be calculated separately.Accurate accounting of the weight of the basic load is the first step to avoid the rated capacity of the crane is too small and hidden overload occurs.

    Load dimensions

    The length, width and height of the load directly affect the hoisting radius, the layout of the hoisting point and the actual effective load of the crane, which is a key factor that can easily be ignored.Large-size, ultra-long, ultra-wide, and ultra-high special-shaped loads will change the force balance of the crane, increase the lifting torque, and directly reduce the actual carrying capacity of the crane.For example, for steel of the same weight, the hoisting requirements of a regular billet are completely different from that of an ultra-long steel truss.Long loads will force the crane to increase the operating radius, and the rated load of the crane will decrease as the operating radius increases.Ultra-wide and ultra-high loads are prone to center of gravity shift, resulting in uneven force. Not only does it require a larger rated capacity, but it also needs to match special spreaders to indirectly increase the overall load requirements.Therefore, the load size is an important basis for correcting the crane capacity parameters.

    Lifting height

    Lifting height refers to the vertical distance of the crane hook manufactured by Henan Mine Crane from the lowest operating position to the highest operating position. The higher the height, the higher the performance and load margin requirements of the crane.In high-lift hoisting operations, wire rope stretching, spreader deformation, and wind load effects will be magnified, and the effective carrying efficiency of the equipment will decrease slightly.At the same time, the lifting height determines the extension length of the crane boom. The longer the boom is extended, the lower the overall stability of the equipment and the higher the safety redundancy requirements.If you only select the type according to the weight of the low-altitude hoisting and ignore the performance loss of the high-lift, it will lead to insufficient actual bearing capacity of the crane during high-altitude operation, and there will be problems of hoisting jitter, overload alarm or even inability to complete the operation.

    Duty cycle

    The frequency of working conditions is the operating frequency of the crane, the length of continuous working time and the number of starts and stops, which directly determines the working level and continuous carrying capacity of the equipment.The hoisting requirements of different projects vary greatly. Temporary single hoisting, daily intermittent operations, and 24-hour continuous high-frequency operations have completely different crane capacity selection criteria.For low-frequency temporary operations, the type can be selected according to the standard rated load.In high-frequency cyclic operation scenarios such as factory assembly lines, port loading and unloading, steel workshops, etc., cranes are under fatigue conditions of start-stop, lifting, and luffing for a long time, and equipment components are lost faster, and the carrying stability will gradually decrease.In such scenarios, a larger load margin must be reserved and a higher rated capacity must be selected to avoid the attenuation of equipment carrying capacity and frequent failures caused by long-term high-frequency operations.

    Operating conditions

    Outdoor open air, indoor airtight, high temperature, low temperature, dust, high wind, humidity, corrosion and other operating environments will directly affect the actual carrying performance of the crane, which is an important correction parameter for capacity calculation.Indoor windless, constant temperature, clean operating environment, stable equipment performance, can be calculated according to standard parameters.In complex outdoor and special industrial environments, load redundancy must be increased.For example, outdoor windy weather will produce lateral wind loads, which will increase the lifting force load.The high temperature environment of steel plants will reduce the stability of metal structures and electrical components.The humid and corrosive environment of chemical industry and coastal areas will accelerate the aging of equipment components.Under harsh working conditions, the effective carrying capacity of the crane will be greatly reduced. If the capacity standards are not adjusted according to the environment, safety risks will easily arise.

    Future load needs

    The professional Henan Mine Crane manufactured crane capacity selection is by no means only to meet the current operating needs. It must take into account future needs such as late-stage expansion of the project, upgrading of working conditions, and material weight gain, and adapt to long-term production and operation.In order to save costs in the short term, many companies choose small-tonnage cranes that just match the current load. After the production capacity is upgraded and the material weight is increased in the later stage, the equipment is directly scrapped or frequently overloaded, resulting in high costs for secondary procurement and transformation.In the scenarios of factory expansion, production line upgrading, port throughput improvement, and equipment iteration, 10%-20% of the rated capacity margin is reserved in advance, which can allow the crane to adapt to changes in working conditions in the next 3-5 years, extend the service life of the equipment, avoid repeated investment, and improve the cost performance of the equipment.

    crane capacity calculation

    How to Calculate the Right Crane Capacity

    After mastering the core influencing factors, it is necessary to follow a standardized and scientific calculation process to accurately calculate the crane capacity required for the project.The industry-common crane load calculation method combines the four core dimensions of basic load, ancillary equipment, dynamic loss, and safety margin. It can be landed and reused throughout the process, and is suitable for all kinds of crane models.The following is a complete disassembly of the calculation steps for everyone, with practical cases attached, which is convenient for direct application.

    Find maximum load

    The first step is to accurately count the maximum static load in the project operation, that is, the net weight of the heaviest material hoisted by the project in a single time, including all non-separable weights such as the material body, fixed accessories, and ancillary components.The statistics need to cover all hoisting conditions in the whole cycle of the project. They cannot only refer to conventional light-load conditions, but must be based on the maximum limit load.For example, for plant equipment installation projects, the weight of conventional hoisting materials is 5 tons, but the weight of the core host equipment is 8 tons. At this time, 8 tons must be used as the maximum basic load, not the average load.At the same time, the position of the center of gravity of the material needs to be checked, and the eccentric load needs to be additionally marked to provide a basis for subsequent margin calculations.

    Add lifting gear

    This is the most easily missed calculation step.Many users only calculate the weight of the material, ignoring the weight of all hoisting auxiliary equipment such as spreaders, wire ropes, hooks, beams, shackles, fixtures, etc., resulting in a small final selection capacity.The weight of all equipment involved in hoisting and lifting synchronously with the load must all be included in the total static load.Under conventional working conditions, the weight of the complete set of spreaders accounts for about 3%-8% of the basic load, and under large-scale special-shaped hoisting and ultra-long hanging beams, the proportion can reach more than 10%.The complete formula is total static load = maximum material load + weight of all spreaders and ancillary lifting equipment.

    Consider dynamic loads

    Static load only represents the weight of the equipment in the stationary state, while the actual lifting process of start-stop, lifting, luffing, rotation, braking and other actions will produce inertial impact and form dynamic loads. This is the core reason for load fluctuations in hoisting operations.The dynamic load will instantly increase the force of the equipment, far exceeding the static rated value.According to industry standards, the dynamic load coefficient of conventional smooth operation is 1.1.The dynamic coefficient of frequent start and stop, rapid lifting, and hoisting of special-shaped materials is 1.2-1.3.In outdoor windy and bumpy operation scenarios, the dynamic coefficient needs to be increased to more than 1.3.The dynamic load calculation formula is total dynamic load = total static load × dynamic load coefficient.

    Apply safety margin

    Safety margin is the core barrier to ensure the long-term safe and stable operation of cranes, and it is also a mandatory requirement of the industry.No matter what kind of working conditions, the crane is not allowed to operate at full load or overload. Reasonable safety redundancy must be reserved to offset the load fluctuations caused by environment, wear and tear, and operating errors.For ordinary indoor low-frequency operations, the safety margin coefficient is recommended to take 1.25.For outdoor conventional construction and medium-frequency operations, the coefficient is 1.3-1.4.In harsh working conditions such as high temperature, corrosion, high-frequency heavy-duty, and high-altitude operation, the safety factor must reach 1.5 and above.The final required crane rated capacity = dynamic total load × safety margin coefficient.This value is the minimum lifting machine tonnage standard adapted to the project.

    How to Choose Crane Capacity for Different Applications

    The operating environment, frequency of operating conditions, and load characteristics of different application scenarios vary greatly, and a unified capacity selection standard cannot be applied.For mainstream crane equipment in various industries, we have compiled targeted capacity selection plans to accurately adapt to the needs of various segmented scenarios.

    Factory overhead cranes

    Henan Mine Crane manufactured plant bridge cranes are mostly used for indoor workshops, production line material transfer, equipment installation and maintenance. The operating environment is stable, there is no wind and rain interference, and the temperature is controllable. They are mainly used for intermittent and regular hoisting.The selection core is adapted to the conventional load of production, while taking into account the future upgrade needs of the production line.In the light-duty parts processing workshop, the calculated rated capacity can directly match the standard tonnage, and the safety factor can be 1.25.In high-frequency operation scenarios of heavy machinery and mold workshops, the capacity margin needs to be increased by 10%-15% to avoid long-term fatigue operation losses.For bridge cranes with continuous cycle operation of assembly lines, priority is given to high-specification models with working levels A5-A7, and more than 20% of the capacity is reserved for redundancy.

    Outdoor gantry cranes

    Outdoor gantry cranes are mostly used for site construction, material depots, and hoisting prefabricated components. They are exposed to wind, rain, sand, and temperature differences for a long time in a complex environment. They are greatly affected by wind load, ground settlement, and temperature deformation, and the load reduction is obvious.When selecting the model, it is necessary to add additional environmental redundancy on the basis of standard computing capacity, with a dynamic coefficient of not less than 1.2 and a safety coefficient of not less than 1.3.For conventional operations in small and medium-sized depots, the type can be selected according to the calculated value of 15% increase.For large-scale infrastructure and high-altitude prefabricated parts hoisting scenarios, they must float more than 20% of their capacity, while matching windproof, non-slip, and anti-tilt configurations to ensure stable operation in complex outdoor working conditions.

    Port cranes

    Henan Mine Crane manufactured port cranes are suitable for container, bulk cargo, and grocery loading and unloading operations. The core characteristics are high frequency, high intensity, long duration, large load fluctuations, and high seaside humidity, salt spray corrosion, and frequent windy weather. The equipment loss rate is much higher than that of ordinary scenarios.The selection of port equipment is strictly prohibited. The selection of full configuration must be based on the maximum limit load, the dynamic coefficient shall be 1.3 and above, and the safety factor shall not be less than 1.4.Container hoisting needs to take into account the dynamic impact of alternating full load and no load. Bulk cargo hoisting needs to consider the load deviation of uneven material center of gravity. The overall capacity needs to be reserved on the basis of the calculated value. 25%-30% redundancy, suitable for 24-hour uninterrupted operation requirements.

    Steel mill cranes

    Steel mill cranes are special heavy-duty equipment, which are used for the transfer of molten steel, billet, and steel. The operating environment is high temperature, dusty, strong thermal radiation, and harsh working conditions. The stability and carrying safety of the equipment are extremely demanding, and they belong to high-risk operating scenarios.The capacity selection of such equipment must be strictly high-standard, and even if the conventional load is small, it must match the large redundant tonnage.The dynamic load coefficient is uniformly taken at 1.3-1.5, and the safety factor is not less than 1.5. At the same time, the strength reduction of steel and equipment fatigue loss in high temperature environments need to be considered.All steel mill cranes need to reserve more than 30% of the capacity margin to eliminate any overload risk and ensure absolute safety under high temperature and heavy load conditions.

    Heavy-duty cranes

    Henan Mine Crane manufactured heavy-duty cranes are mainly used in heavy-load scenarios such as large-scale infrastructure, wind power installation, large-scale equipment hoisting, and bridge construction. The hoisting load is large, the operating radius is large, the lifting height is high, and the operation is difficult. The value of a single hoisting is high and the risk is high.The selection of heavy equipment needs to be combined with accurate torque calculation, operating radius correction, and high-altitude wind load correction. The selection of heavy equipment cannot be based on the basic weight alone.All heavy-duty operations must review the torque curve and reserve sufficient margin within the rated torque range. The capacity selection must be based on the accurately calculated value and rise by more than 30%. At the same time, it matches professional counterweight, spreader and operation plan to avoid the safety risks of high-altitude heavy-duty hoisting.

    What Happens If You Choose the Wrong Crane Capacity?

    The deviation of crane capacity selection is divided into two situations: the tonnage is too small and the tonnage is too large. Both will have a negative impact on the project, especially the selection of small tonnage overload, which will cause multiple problems of safety, cost, efficiency, and equipment loss, which directly affect the overall project revenue and construction safety.

    Overload risks

    This is the most deadly hazard of improper selection.Insufficient rated capacity of the crane will lead to long-term overload operation of the equipment, exceeding the carrying limit of the fuselage metal structure, wire rope, reducer, and reel, which can easily cause major safety accidents such as wire rope fracture, boom bending, main beam deformation, and overturning of the whole machine.At the same time, the safety protection device of the equipment under overload will frequently alarm and self-lock and stop. Forced operation will directly lead to equipment scrap, material damage, and even cause casualties, bringing irreversible safety accidents and legal responsibilities.

    Higher costs

    The tonnage selection is too small, which will cause the equipment to fail to meet the operating needs. It is necessary to temporarily lease large-scale equipment, replace spreaders, and adjust the construction plan, resulting in additional leasing, labor, and construction period rectification costs.Equipment that is severely overloaded and damaged will also have to bear high maintenance and replacement parts costs.On the contrary, blindly choosing oversized tonnage cranes will cause equipment procurement and leasing costs to be inflated, large-scale equipment will consume more energy, operation and maintenance costs will be more expensive, and long-term idleness will be wasted, which will significantly compress the profit margins of the project and cause a waste of capital and resources.

    Lower efficiency

    Cranes with insufficient capacity frequently trigger overload protection, start-stop caton, and slow lifting during operation. The time-consuming of a single hoisting is greatly increased, which cannot match the pace of project construction and directly slows down the overall construction period.Some overweight materials cannot be hoisted in place at once, and they need to be split and hoisted multiple times, which greatly increases the process and reduces the efficiency of the operation.For cranes with excessive tonnage, the equipment is large in size, the operating flexibility is poor, and the lifting of light materials has the problems of redundant operation and slow movement, which will also reduce the efficiency of daily operations and affect the overall progress of the project.

    Faster wear

    Long-term overload operation is the core cause of premature aging of crane equipment.When the rated capacity is insufficient, the metal structure, transmission components, and electrical system of the fuselage are in a state of overload and fatigue for a long time, and the wear rate is doubled. Problems such as wire rope aging, bearing wear, main beam deformation, and electrical failure occur frequently.Even if there is no safety accident, the equipment failure rate will be greatly increased and the service life will be greatly shortened. Equipment that could have been used for 10 years may be completely scrapped in 3-5 years, greatly increasing the cost of equipment iteration of enterprises and affecting production continuity.

    Henan Mine Crane Factory Custom

    The calculation and selection of crane capacity is the core work that takes into account construction safety, operating efficiency, project cost, and equipment life. It is by no means a simple weight matching.From basic load, spreader weight, dynamic loss to safety margin, from indoor factories and outdoor depots to special scenes in ports and steel plants, each parameter and each type of working condition has its own calculation and selection criteria.Accurate accounting of crane capacity can not only completely avoid overload safety risks, reduce equipment losses, but also maximize project cost control and improve operational efficiency. It is an indispensable core link before various engineering projects are implemented.Henan Mine Crane Factory can obtain a one-to-one accurate crane tonnage selection plan according to the specific working conditions, hoisting parameters, and operating environment of your project.

    Henan Mine CraneDiscuss your requirements ↗
  • How Rubber Tyred Gantry Cranes Maneuver Efficiently in Limited Workspaces

    How Rubber Tyred Gantry Cranes Maneuver Efficiently in Limited Workspaces

    How Rubber Tyred Gantry Cranes Maneuver Efficiently in Limited Workspaces

    Rubber Tyred Gantry Cranes (RTG) are the core container handling equipment in container terminals and logistics yards where space is at a premium. Many logistics planners and yard managers will have this question: how can a heavy equipment with dozens of tons of weight and huge load capacity flexibly travel in a narrow yard and efficiently complete the loading, unloading and stacking of containers?

    With the increasingly tight land resources, many yards have to increase the density of container storage, the operating space is further compressed – the distance between the rows of containers is getting narrower and narrower, and the operating channel is also constantly shrinking. This puts high demands on the maneuverability of RTG cranes.

    In fact, tire gantry cranes (RTG) can work efficiently in limited space, the core lies in its steering system, travel mode, structural design and intelligent control of the synergistic cooperation.

    What Is a Rubber Tyred Gantry Crane?

    Basic Definition

    Rubber Tyred Gantry Crane, or RTG Crane for short, is a kind of mobile gantry crane with rubber tires as the traveling device. Its core structure is similar to that of an ordinary gantry crane, with main girder, outriggers, hoisting mechanism and trolley system, but the biggest difference is that it doesn’t need to rely on fixed rails, and can move freely on the level ground.

    It is mainly used for container handling in container yards and logistics centers, and its core function is to complete the stacking, loading and unloading of containers, as well as the transfer between different areas. Compared with rail-mounted gantry cranes (RMG), its biggest advantage is its flexibility, which is not restricted by tracks and can be adapted to various complex yard layouts.

    Key Features

    Rubber tire mobility is its core feature. The use of high-strength rubber tires and the hydraulic drive system allow the RTG to withstand huge deadweight and lifting loads while moving smoothly on level ground without the need to lay special tracks, which significantly reduces the cost of site modification.

    The independent travel system allows each tire of the RTG to be controlled independently, which is the basis for its ability to steer flexibly. Even in narrow aisles, accurate positioning and movement can be accomplished by adjusting wheel steering.

    Adapting to flexible yard layout, no matter it is a regular rectangular yard or an irregular temporary yard, RTG can quickly adapt to it without having to readjust the equipment or the site due to the change of layout, which saves a lot of time.

    Higher stacking capacity, capable of stacking containers up to 4-6 levels, maximizes the use of vertical space in the limited floor space and increases the storage capacity of the yard, which is one of the reasons for its popularity in space-constrained yards.

    Why Maneuverability Matters in Limited Workspaces

    Increasing Container Yard Density

    Nowadays, land resources in ports and logistics yards are getting tighter and tighter, especially in coastal ports, where the cost of land is extremely high and unlimited expansion of yard area is not possible. In order to increase throughput, the container yard density can only be increased continuously.

    This results in the spacing between rows of containers shrinking and the operating aisles becoming narrower. If the RTG’s maneuverability is not good, and it cannot turn around and move between the dense containers, the operation progress will be seriously affected, and even the lifting operation cannot be completed.

    Operational Efficiency

    The operational efficiency of the yard directly depends on the movement and lifting speed of the RTG. In the limited space, the better the mobility of the RTG, the faster it can complete the loading and unloading of containers, transfer and stacking, and shorten the processing cycle of a single container.

    If the maneuverability is insufficient, the RTG needs to repeatedly adjust its position to complete a lifting, which not only wastes time, but also leads to traffic congestion inside the yard, affecting the passage of other operating vehicles and further reducing the overall operational efficiency.

    Safety Considerations

    In the limited space, the containers are piled up densely, and there are also forklifts, container trucks and other operating vehicles, so the operating environment is very complicated, and the mobility of RTG is directly related to the safety of the operation.

    If the RTG is not flexible in steering and moving accurately, it is easy to collide with the surrounding containers and operating vehicles, which will not only damage the equipment and goods, but also may cause casualties. Good maneuverability allows RTGs to control their position accurately in narrow spaces and avoid collisions.

    Advanced Steering Systems in RTG Cranes

    The core reason why RTG can maneuver flexibly in limited space is its advanced steering system. Unlike ordinary vehicles that only have front wheel steering, RTG adopts multi-wheel independent steering design with multiple steering modes to cope with various needs in narrow spaces.

    Multi-Wheel Steering Design

    Most RTGs adopt a multi-wheel steering design, where each wheel on the bottom of the outrigger can adjust the steering angle independently, rather than in a fixed direction. This design allows RTGs to steer much more flexibly without the need for a large turning space as in a normal vehicle.

    For example, in narrow container rows, the RTG can realize small-scale steering and movement by adjusting the steering angles of different wheels, without having to make large adjustments backward or forward, which saves operating space and time.

    Crab Steering Mode

    Crab Steering Mode is RTG’s specialty in limited space and one of its most unique steering modes. When this mode is turned on, all wheels will be synchronized to turn 90 degrees, and then the RTG can move sideways like a crab along the direction perpendicular to the main beam.

    This side-to-side movement can accurately align the stacking position of the containers without adjusting the position back and forth, which is especially suitable for adjusting the working position between narrow container rows, avoiding the inability to get close to the target containers due to the limited space.

    Pivot Steering

    The pivot steering mode allows the RTG to rotate around a center point with a particularly small turning radius. This center point can be the center of the crane or the wheels of a certain set of outriggers, which can be adjusted according to the operating scenario.

    In areas where space is extremely limited, such as corners of yards and narrow passages, pivot steering allows the RTG to change direction quickly without taking up too much operating space, avoiding hitting surrounding obstacles due to a large turning radius.

    Coordinated Steering Control

    The steering system of RTG adopts electronic synchronized control technology, all the wheels’ steering movements are precisely coordinated through the control system to ensure the steering process is smooth and precise, without any wheel shift or stuttering.

    This coordinated control enables the RTG to keep its body stable during steering and moving, especially when lifting heavy objects, which will not be tilted due to unstable steering, thus not only ensuring the safety of the operation, but also improving the accuracy of the operation.

    Flexible Travel Modes That Improve Maneuverability

    In addition to the advanced steering system, RTG is also equipped with a variety of flexible travel modes, different travel modes are suitable for different operating scenarios, which further improves its maneuverability in limited space and makes the operation more efficient.

    Straight Travel Mode

    Straight Travel Mode is the most commonly used travel mode of RTG. When this mode is turned on, all the wheels remain in the same direction and the crane travels in a straight line, which is mainly used for moving back and forth in the passage between container rows to complete the loading and unloading of containers and transshipment.

    In this mode, RTG’s traveling speed is stable, can quickly switch between different operating points, suitable for large, regular layout of the yard operation, although simple, but can ensure the efficiency of basic operations.

    Diagonal Travel Mode

    Diagonal Travel Mode is one of the key modes for RTG to enhance operational efficiency. When this mode is turned on, the RTG will move in a diagonal direction, without having to travel in a straight line and then make a turn, so that it can move directly from one container row to another.

    In the limited space, this traveling mode can save a lot of time for adjusting the position, especially in the case of irregular layout of the yard and narrow aisles, diagonal turning can avoid repeated adjustments of the direction, which greatly improves the operational efficiency.

    Rotational Turning

    Rotational turning mode is similar to pivot turning, but it has a larger rotating angle, which allows the RTG to complete a 360-degree rotation in place, or to adjust any angle of steering according to demand.

    This mode is suitable for use in extremely narrow spaces, such as the corners of the yard, equipment-intensive areas, where the RTG can quickly change the direction of operation by rotational turning, without taking up additional operating space and avoiding collision with the surrounding equipment and containers.

    Compact Structural Design for Space Optimization

    In addition to the steering and driving modes, the compact structural design of RTG plays a key role in its ability to operate efficiently in limited space. When designing, the engineers will try to optimize the structure under the premise of guaranteeing the structural strength and bearing capacity, so as to reduce the footprint of the equipment and improve the space utilization rate.

    Optimized Wheelbase

    The wheelbase of RTG is precisely optimized, neither too long nor too short. A long wheelbase will increase the turning radius, which is not conducive to steering in narrow spaces; while a short wheelbase will affect the stability of the equipment and make it easy to tilt when heavy loads are lifted.

    The optimized wheelbase not only ensures the stability of the RTG during the lifting operation, but also minimizes the turning radius, allowing it to steer and move flexibly in narrow passages.

    Lightweight but Strong Frame Design

    The frame of RTG is made of high-strength steel, which ensures the structural strength and ability to withstand huge lifting loads, while minimizing the weight of the equipment. The lightweight design not only reduces the wear and tear of the tires, but also allows the equipment to move more flexibly without being too heavy and clumsy.

    At the same time, the structure of the frame is very compact, the main beam and legs are well laid out and do not take up too much space, allowing the RTG to move flexibly between narrow rows of containers without being restricted by space due to its large structure.

    Adjustable Span Configurations

    Different yards have different container arrangement widths, stacking methods, and operating spaces, RTG adopts an adjustable span design, which allows the span of the main beam to be adjusted according to the layout of the yard and the size of the containers.

    This adjustable design allows the RTG to adapt to different yard layouts without wasting operating space due to a fixed span, and without the need to replace the equipment in order to adapt to the site, which greatly improves the versatility of the equipment and the utilization of space.

    Intelligent Control Systems That Improve Navigation

    Modern RTG cranes are equipped with intelligent control systems that help operators control the equipment more accurately, improve navigation and maneuverability in limited space, reduce human error, and improve operational safety.

    GPS and Automated Guidance Systems

    Many RTGs are equipped with GPS and Automated Guidance Systems, which can accurately locate the crane’s position in the yard within centimeters. Through the control system, the operator can clearly see the real-time position of the RTG, as well as the distribution of the surrounding containers and operating vehicles.

    This accurate positioning allows the operator to quickly find the target container without having to repeatedly adjust the position, especially in dense yards, avoiding the waste of space and time due to inaccurate positioning and improving operational efficiency.

    Anti-Collision Systems

    In a limited space, where the operating environment is complex and the risk of collision is high, RTG’s anti-collision system detects obstacles in real time through sensors, radar and other technologies, including containers, operating vehicles, personnel and so on.

    Once the distance between the RTG and the obstacle is detected to be too close, the system will automatically send out an alarm to remind the operator to slow down or stop the operation; if the operator does not react in time, the system will automatically slow down and stop to avoid collision accidents and ensure the safety of the operation.

    Automated RTG Operations

    Many RTGs nowadays support remote operation or semi-automated control. The operator can control all the actions of the RTG through the screen in the control room, without having to follow the equipment on site, which not only improves the operational efficiency, but also reduces the safety risks of on-site operation.

    Semi-automated or fully-automated operation reduces human errors and allows RTGs to move, steer, and lift more accurately, especially in limited spaces, avoiding wasted space or safety accidents caused by human errors.

    Operational Advantages of RTG Cranes in Limited Spaces

    Combined with the steering system, traveling mode, structural design and intelligent control mentioned above, the operational advantages of RTG in limited spaces are very obvious, which makes it the preferred equipment for yards and terminals where space is tight.

    High Container Stacking Efficiency

    The stacking height of RTG can reach 4-6 levels, which is higher than the stacking height of ordinary lifting equipment. In the limited ground space, it can maximize the use of vertical space, significantly increase the storage capacity of the yard, and solve the problem of land resources.

    At the same time, its precise maneuver ability can make the containers stacked more neatly and densely, which further improves the space utilization and allows the limited yard to accommodate more containers.

    Flexible Yard Layout Adaptation

    Unlike rail-mounted gantry cranes (RMG), RTGs do not rely on fixed rails and can move freely on level ground. Whether the yard layout is regular or irregular, temporary or fixed, RTGs can adapt quickly.

    If the layout of the yard needs to be adjusted, RTG can directly adjust the working route without re-laying the track, which saves a lot of time and infrastructure costs, especially suitable for temporary yards that need to adjust the layout frequently.

    Reduced Infrastructure Requirements

    One of the biggest advantages of RTG is that it does not require the laying of fixed tracks. Compared with RMG, it eliminates the need for infrastructure investment for track laying and does not affect the layout and operation of the yard due to the space occupied by the track.

    As long as the yard floor is smooth and can bear the weight of RTG, it can be put into use directly, which greatly reduces the cost and cycle of site reconstruction, especially suitable for small yards or temporary operation sites where space is limited and tracks cannot be laid.

    Typical Applications Where Space Efficiency Matters

    RTG’s flexible maneuverability and space-optimized design make it play an important role in many space-constrained scenarios, especially where space utilization and operational efficiency are highly demanded.

    Container Terminals

    Container terminals are the most important applications for RTG. The land resources of the terminal are extremely tight, the density of container stacking is extremely high, the aisle between rows is narrow, and the operation is fast-paced.

    RTG’s flexible steering and moving ability can quickly shuttle between dense containers to complete container loading, unloading, stacking and transshipment, which not only ensures operational efficiency, but also maximizes the use of limited space at the terminal.

    Intermodal Logistics Yards

    Intermodal logistics yards need to connect railroads and trucks for container transshipment, and the operation space is relatively complicated, with both container storage and loading/unloading areas, which makes the space very tight.

    RTG’s flexible maneuver capability can quickly switch between different areas to complete the container transfer without affecting the efficiency of the railroad and truck connection due to limited space, thus improving the overall speed of intermodal transportation.

    Precast Concrete Yards

    In precast concrete yards, precast panels, precast beams and other components are large in size and heavy in weight, so the space in the yard is often tight, and the density of components stacked is also high.

    The RTG’s high load carrying capacity and flexible maneuverability allow it to accurately handle these heavy components and move flexibly in narrow yards, avoiding collisions between components while maximizing the use of yard space.

    Industrial Equipment Storage Yards

    Industrial equipment storage yards are densely packed with large machinery and heavy components, with limited operating space and frequent adjustments to the position of equipment and components.

    RTG’s flexible movement and precise lifting ability can complete the handling and storage of large equipment and parts in a narrow space, adapting to the limited space of the site and improving the operational efficiency of the yard.

    Key Factors When Choosing an RTG Crane for Limited Workspaces

    If you need to choose an RTG crane for limited workspace, you don’t need to blindly pursue high configuration, but focus on the following key factors in combination with your own operational needs, so that you can choose the most suitable equipment.

    Wheel configuration is the basis, give priority to multi-wheel independent steering configuration, the number of wheels and layout will directly affect the maneuver ability of RTG, multi-wheel independent steering RTG, more flexible in narrow space.

    The design of steering system is very critical, choose the RTG equipped with crab steering and pivot steering modes, these steering modes allow the equipment to quickly adjust the position in the limited space and improve the operational efficiency.

    Turning radius capability, according to the width of the yard channel to choose the appropriate turning radius, the smaller the turning radius, RTG in the narrow space, the better the flexibility, the more adapted to the layout of the dense yard.

    The level of automation, according to the operational needs to choose, high-frequency, high-precision operations, you can choose semi-automated or fully automated RTGs, which can reduce human error, improve operational efficiency and safety.

    Compatibility of yard layout, choose the RTG with adjustable span to ensure that the equipment can adapt to the yard layout and container size, avoiding the waste of space due to the fixed span.

    Frequently Asked Questions

    Combined with the usual experience of receiving customers, I have organized a few of the most frequently asked questions and answered them in an easy-to-understand way to help you quickly clear up the key questions about RTG operation in limited space.

    How many steering modes does an RTG crane typically have?

    Conventional RTG cranes usually have 4 steering modes, namely straight line steering, crab steering, pivot steering and diagonal steering. Different steering modes are adapted to different operating scenarios, especially crab and pivot steering, which are especially practical in limited space and can greatly enhance the maneuverability.

    What is the turning radius of a rubber tyred gantry crane?

    There is no fixed value for the turning radius of an RTG, it depends on the wheelbase and wheel configuration of the machine, the turning radius of a regular model is around 5-8 meters. With pivot steering, the turning radius can be even smaller, and even in-situ rotation can be realized, which is especially suitable for narrow spaces.

    Are RTG cranes better than rail-mounted gantry cranes in small yards?

    RTGs are often better than rail-mounted gantry cranes (RMGs) in small yards. This is because RTGs do not need to lay tracks, which saves infrastructure costs and space, and are more flexible and adaptable to the irregular layout of small yards, whereas RMGs need to be fixed on tracks, which takes up extra space and makes it difficult to adjust the layout.

    Can RTG cranes operate automatically?

    Can RTG cranes operate automatically? Nowadays, many RTGs support semi-automated or fully automated operation, which can realize automatic loading and unloading, stacking and transshipment of containers through GPS guidance and automatic control system. Automation not only improves the operation efficiency, but also reduces human error, especially suitable for limited space and intensive operation scenarios.

    What is the typical container stacking capacity of an RTG crane?

    The typical container stacking capacity of an RTG crane is 4-6 layers, depending on the lifting capacity and span of the crane. Smaller RTGs can typically stack up to 4 floors, while heavier RTGs can stack up to 5-6 floors, maximizing the storage capacity of the yard in a limited floor space.

    Conclusion

    RTG cranes can maneuver efficiently in limited space, the core is the advanced steering system, flexible driving mode, compact structural design and intelligent control system, the synergistic cooperation of these four core strengths, so that this heavy equipment can flexibly shuttle in a narrow site, precise operation.

    For container terminals and logistics yards where space is tight, RTG is the ideal equipment to enhance space utilization and operational efficiency. It does not have to rely on fixed tracks and can adapt to various complex layouts, maximizing the use of limited space while ensuring operational safety and efficiency.

    By choosing the right RTG configuration and combining it with your own yard layout and operational needs, you can give full play to its advantages, maximize the value of your limited space, and improve the overall operational efficiency of your yard.

    Call to Action

    If you have limited space in your container yard or logistics site and need a flexible and efficient RTG crane, submit your yard layout, operational requirements and lifting parameters, and we will provide you with customized RTG solutions.

    Henan Mine Crane Factory supply, as a professional crane manufacturer, integrates R&D, design, manufacturing, sales and service to provide customers Please feel free to contact us, we will provide you with free design drawings, and field survey!


    Henan Mine CraneDiscuss your requirements ↗
  • How RTG Cranes Solve the Container Swing Problem

    How RTG Cranes Solve the Container Swing Problem

    How RTG Cranes Solve the Container Swing Problem

    Every operator who has worked an RTG crane knows the frustration: you accelerate the trolley, the container swings forward, you decelerate, it swings back. You wait. The clock ticks. A truck sits idle below. Another crane is blocked in the adjacent bay.

    Container swing—formally called load sway—is one of the most persistent productivity killers in container terminal operations. Industry data shows that waiting for sway to settle can occupy more than one-third of the entire move time for less experienced operators. In a terminal handling hundreds of thousands of TEUs per year, that lost time compounds into millions of dollars in avoidable cost.

    What Is Container Swing?

    Container swing in an RTG crane is a classic pendulum effect. A container suspended from the trolley via wire ropes behaves exactly like a pendulum bob on a string: once displaced from vertical, it oscillates back and forth until friction gradually brings it to rest.

    The physics are straightforward. The pendulum period—the time for one full back-and-forth cycle—depends only on rope length, not on container weight. Longer ropes (i.e., greater hoist height) produce slower, longer swings that are harder to manage manually.

    Swing is induced whenever the trolley or crane gantry accelerates or decelerates. When the trolley moves forward, the container lags behind, then overshoots when the trolley stops. At the end of a travel movement, the container continues forward to the end of its arc, reverses, and oscillates until damped. Wind load, jerky operator inputs, and uneven yard surfaces compound the problem.

    The primary causes of RTG container swing include:

    • Sudden acceleration or decelerationof the trolley or gantry
    • High travel speedsover long distances
    • Wind or environmental disturbancesacting laterally on the container
    • Jerky or inexperienced operator inputs
    • Variable rope lengthas containers are hoisted to different heights across a stacking block

    For container handling, accurate placement must be precise to within a few millimeters. Any residual swing at the end of a move must be fully damped before the spreader can be lowered onto the target container. This is the core productivity cost of uncontrolled sway.

    What Causes Container Sway in RTG Crane Operations?

    Before exploring solutions, it is worth understanding the scale of the problem. Industry sources indicate that countering sway can occupy up to 30% of the average move time during container handling operations. For a crane completing 25 moves per hour, that is the equivalent of losing 7–8 productive moves per hour to swing management alone.

    The impact is not evenly distributed. Experienced operators can “drive into the swing”—actively compensating by jogging the trolley in the direction of sway to damp the oscillation. Only the most skilled operators can simultaneously kill sway and position the load in a single continuous motion. Everyone else completes these as two separate operations: kill the swing first, then fine-position.

    Beyond productivity, uncontrolled container swing creates direct safety risks: containers can collide with adjacent stacks, damage spreaders, strike truck trailers in the landside lane, or injure ground personnel. In automated RTG operations, residual swing is simply incompatible with the precision required for unattended placement—making anti-sway technology a functional prerequisite for any automation program.

    The economic calculus is clear. Anti-sway technology is not a luxury upgrade. It is a core productivity and safety investment that pays back quickly in high-throughput terminals.

    Which RTG Anti-Sway Solutions Are Available?

    RTG crane anti-sway technology has evolved through three distinct solution families. Each has different cost profiles, maintenance requirements, and effectiveness characteristics.

    1. Mechanical and Hydraulic Passive Damping Systems

    The earliest approach to container swing control was entirely mechanical. These systems use special hoist reeving geometry or physical damper mechanisms to resist swing forces directly on the spreader or head block.

    Hydraulic sway damping systems—historically common on RTG cranes, with systems produced by suppliers such as Italy’s Rima Group—use inclined auxiliary ropes connected between the spreader or head block and hydraulic cylinders on the trolley. When the container swings, the ropes go taut and the hydraulic circuit absorbs and dissipates the sway energy. These are passive systems: they damp existing sway but cannot prevent it from initiating.

    The limitations of hydraulic and mechanical passive systems are significant:

    • The following is one way of assuming the dampening process to work: They cannot stop the swing beginning but can dampen it after.
    • Once the trolley has stopped, the operator is still required to wait for the hydraulic damping to settle before lowering the container
    • They have elevated maintenance levels to take into account: hydraulic systems, seals, cylinders and rope elements all need financial investment to keep maintained
    • Effective only in one direction unless a multi-axis reeving scheme is introduced.

    When dealing with current high-throughput processes, passive hydraulic damping is treated as an old standard that is not as effective as more advanced techniques.

    2. Electronic Open-Loop (Feedforward) Control Systems

    The use of VFD’s and PLC’s on crane drives has made electronic only solutions practical. Open loop anti-sway systems essentially mathematically manipulate the crane’s motion profile to avoid pole effects10.

    The system uses a mathematical model of pendulum dynamics—taking rope length (derived from hoist drum encoder position) and load characteristics as inputs—to calculate an optimized acceleration/deceleration curve for every trolley movement. Rather than applying a simple ramp-up/ramp-down velocity profile, the system shapes the motion so that the resulting pendulum forces cancel each other out by the time the trolley reaches its destination.

    Open-loop systems require no additional sensors on the load itself. The PLC predicts behavior based on the motion model and issues corrective drive commands proactively. The key advantage is simplicity: no sway angle sensors to maintain, no closed-loop feedback latency.

    The critical limitation: open-loop systems cannot respond to external disturbances such as wind or impacts, because there is no measurement of actual load position. If the container swings for a reason the model did not predict, the system cannot correct it. Open-loop electronic anti-sway is best suited for indoor or sheltered operations where wind loading is not a factor.

    3. Closed-Loop Active Feedback Systems (Best Practice for RTG)

    The most widely used method for outdoor operating RTG’s is an active closed loop anti sway system that uses real time sensor feedback with feedforward control. This system address both internally induced sway, from the crane movements, and externally induced sway, from external forces such as the wind.

    These systems combine several components:

    • Inclinometers / sway sensors will record the actual swing angle of the load.
    • The motion state data can be read from transport state by hoist encoders and trolley position sensors.
    • Load cells can be used for rough card control or to convert container weight to a new control parameter. To use it in either of these ways a load cell must be calibrated against the weight of an empty container.
    • The PLC takes all of the sensor data and performs the combined feedback + feedforward control algorithm.
    • The VFDs on the trolley and hoist drives respond to the corrective speed and acceleration commands in 5-10 msec.

    Overall control logic is a continuous loop. The feedforward (planning) compensates for anticipated sway and thus prevents it. The feedback (correction) compensates for any residual sway in the container whatever its source (including swing induced by a rate command to a passive load, like a container). The container arrives at the target, pretty much free of residual swing, immediately ready to be lowered.

    How Do Leading RTG Crane Manufacturers Reduce Container Swing?

    Konecranes: Active Load Control (ALC)

    Konecranes has also invented something called Active Load Control (ALC) a proprietary technology which Konecranes claim all but removes container sway. ALC is a closed-loop actively managed, predefined motion system implemented into the RTG’s main control system. It utilizes intelligent profiles together with real time sway detection so that the operator can handle rough yard surface conditions, whether working manually or fully automated.

    ALC for automation to support the ARTG (Automated RTG) systems of Konecranes, who claim that automation without it cannot be true automation as the best possible automated container placement cannot be achieved. And any terminal with Konecranes RTGs and ALC can then move onto full automation, without changing the yard equipment the sway control has been built-in and proven.

    Liebherr: Eight-Rope Anti-Sway Reeving

    Liebherr’s approach to RTG anti-sway combines mechanical reeving geometry with electronic drive control. Their standard RTG configuration features an eight-rope reeving anti-sway system, which distributes the hoist load across a geometry that is inherently more resistant to pendulum oscillation than a simple two-rope or four-rope reeving. Precise simultaneous drive motion control removes the need for a head block or side shift mechanism, further simplifying the lifting interface.

    Konecranes (Earlier System): Hybrid Rope-and-Electronic Approach

    An earlier Konecranes system for RTG cranes—a precursor to the modern ALC—used four AC motor-driven winches controlling four auxiliary ropes reeved from the main hoist rope drum to the head block and back to auxiliary winches on the trolley. The ropes were inclined in both trolley and gantry travel directions, providing sway prevention effectiveness in two axes. Each winch was controlled independently by PLC algorithms. This hybrid solution went hand in hand with the mechanical efficiency of the damping via rope and the intelligence of the electronic control.

    ABB: Dual-Mode Electronic Systems

    ABB currently has two electronic anti-sway products available for use by cranes the first is an closed-loop system designed for outdoor container crane applications that measures load motion to dampen both motion-induced and wind-induced sway, and the second is an open-loop system that is used for indoor overhead crane applications where external disturbances are not present. The closed-loop system is completely integrated into the main PLC control architecture of the crane.

    How Does RTG Anti-Sway Technology Work?

    Knowing the details of the operation of a typical modern closed loop RTG anti-sway system enables terminal engineers, operators and procurement managers to assess system specifications more accurately.

    Step 1: Motion planning When the operator hits a trolley travel switch, the anti sway plc doesn’t respond by directly commanding the full drive speed. Instead it develops an optimal motion profile based on current rope length (from hoist encoder), load weight measurement, distance to travel, and the allowable percentage of sway. This yields a unique acceleration profile for the move.

    Step 2. Feedforward control Based on the current pendulum dynamics model the system calculates the sway it can expect to obtain from the prior moves, and programs the control signals to the VFDs accordingly. The trolley accelerates between stops across a shaped velocity profile – typically reversing and accelerating briefly just before reaching the destination – to null out the pendulum forces at the target.

    Step 3. Feedback sensors in real-time The sway sensors (inclinometers) constantly determine the actual swing angle of the container as it is moved. Trolley position encoders check trolley travel. Load cells observe the target load. All information updates immediately to the control PLC.

    Step 4. Corrective action if feedback sensor indicates the actual sway no longer matches the model (as a result of wind, rough surface etc. or model error), the PLC will send corrective commands to the VFD in milliseconds, such as a small counter-motion “kick” signal, brief speed reduction, or collective tension correction to the hoist.

    Step 5: Zero Sway Arrival The cargo reaches its destination with zero or near-zero residual sway. The operator (or automated controller) may lower the spreader immediately. The control cycle which includes starting to move the cargo, stopping that movement, and arriving at the destination with zero residual sway is completed faster than the operator perceives each separate step.

    What Are the Main Anti-Sway RTG Modes?

    Most modern RTG anti-sway systems are designed to operate in different modes which can be selected according to the type of terminal and automation level:

    Manual anti-sway mode. The operator fully controls the crane’s motion, with the anti-sway system tapping in to even acceleration/deceleration curves and neutralize detected sway. To the operator, the crane feels more docile and stable, without an autonomous system “fighting” him/her.

    Semi-Automatic Mode The operator simply chooses a destination position whereby the anti-sway system automatically takes care of the travel profile and positioning while the operator observes and can take control if necessary. This mode greatly lessens operator skill and fatigue while still retaining a human in the loop.

    In fully-automatic mode (ARTG operation), the anti-sway logic exists within the automated cycle control system. The container pick and place cycle is performed without operator intervention, however the anti-sway system assists at each step.

    How Does Anti-Sway Improve Productivity?

    RTG cranes with anti-sway are viewed by terminal operators as an advantage for utilization of cranes in the following dimensions:

    Throughput increase: Reducing the time operators wait for sway to settle or adjusting it manually allows cycle times per move to drop. Even a 10–15% reduction in average cycle time can lead to a large increase in containers per crane-hour.

    Less skilled: Less-skilled operators are able to place containers with accuracy close to the levels of proficient operators when active anti-sway control assistance is used. Faster training and enhanced operator consistency is achieved.

    Safety enhancement: By ensuring the container is moved in a controlled & predictable manner, the risk of a container to container collision, spreader damage and truck trailer impacts, as well as personnel risk, can be minimized, within the landside lane.

    Less mechanical wear: A smoother, more consistent acceleration and deceleration cycles less fatigue hoist ropes, sheaves, spreader pins and drive components delaying maintenance intervals and lowering replacement costs.

    Automation enablement: For terminals considering the move toward automation for RTG operation, automation enabling of the terminal requires effective sway eliminating. No matter how accurately Automated Container Placement systems position the containers at terminal, they cannot achieve unmanned operation if the process is not accurate enough.

    How to Choose the Right RTG Anti-Sway System?

    Before specifying for RTG crane anti-sway or upgrading the anti-sway capability, terminal operators need to take into account:

    Indoor vs. outdoor operation. RTG yards located outdoors will experience wind loading that cannot be mitigated by open-loop control systems. The appropriate, but more costly, solution is the use of a closed-loop control system with meancaswingfeedback.

    Automation roadmap. If the terminal plans to eventually automate RTGs, the anti-sway must be able to support automated cycle control. Ensure the system is compatible with the RTG’s standard automation-ready control architecture and that a credible OEM upgrade path exists.

    Integrated with other controls. Naturally-integrated anti-sway systems, directly integrated into the crane’s main PLC/VFD house, are more reliable and simplified to operate and maintain than retrofit add-ons with separate local drives and hardware. How does the OEM connect the anti-sway logic to the main drives?

    Sensor maintenance.Closed-loop systems need sway sensors (or inclinometer or whatever). So, what maintenance schedules, failure modes, operation of bot when sensor data is lost? Design that can fail “safe” (back to open-loop) rather than fail/disengage sway control.

    Operator interface and mode selection. Consider how conveniently and intuitively operators will be able to select anti-sway modes, receive the system status, and take over control when necessary. If the HMI is confusing or inaccessible, the technology will not be used effectively.

    Frequently Asked Questions

    Frequently Asked Questions

    Q: What is container swing in an RTG crane? A: Container swing (or load sway) is the swinging of a suspended container caused by the acceleration and deceleration of the trolley or crane gantry. The container swings like a pendulum, being pulled backward or forward of the suspension point until friction slow it down. In RTG cranes it needs to be kept to a minimum for accurate placement.

    Q: How does an RTG crane anti-sway system work? A: The current RTG anti-sway systems incorporate feedfoward control (predicting swing based on the planned motion mathematically) and closed loop feedback (detecting the sway angle with inclinometer sensors). The PLC constantly modifies the trolley velocity profile with Variable Frequency Drives to eliminate the swing before it is initiated and nullify any swing if it occurs.

    Q: How do open loop and closed loop anti-sway systems differ? A: Open loop systems utilize the mathematical model of the crane’s motions to derive a motion profile which is designed not to induce any load swing. There is no direct measurement available of the load’s actual position. External forces such as wind load cannot be compensated for in the open loop system. Closed loop(actively fed back) systems constantly measure the actual sway angle, and react to cancel this in real time. Offlode swing as well as externally induced swing are addressed by a closed loop system. In outdoor RTG function closed-loop systems are implemented.

    Q: How much is container sway costing in terms of throughput? A: The manufacturing industry appears to identify this cost at over 1/3rd of the total move time, if not more, for novice operators. Even experienced workers experienced cost above and beyond in every cycle from anti-sway systems. The throughput benefit would therefore be considerable, clocking in at anywhere from 10–25% on average, depending on new/old baseline.

    Q: Is active sway elimination a functional requirement for RTG automation? A: Yes, in a practical sense. Automated RTG operations require that the spreader can be precisely positioned at the pick or place point with very low residual sway levels so that the vision and the positioning systems can detect and effectively interface with the container corner castings. Therefore active sway reduction/imposition is a functional requirement rather than an additional feature.

    Henan Mine Crane Factory Custom

    Container swing remains one of the biggest challenges in container yard operations, directly affecting handling efficiency, operational safety, and automation performance. Modern RTG cranes equipped with advanced anti-sway technology can significantly reduce load oscillation, enabling faster, safer, and more precise container handling.

    Henan Mine Crane Factory supply RTG cranes are engineered with intelligent anti-sway control systems, high-precision sensors, and automation-ready designs to help terminals achieve smoother operations, shorter cycle times, and lower maintenance costs. Whether operating in busy ports, rail terminals, or intermodal logistics hubs, our solutions are built to deliver reliable performance under demanding conditions.

    With decades of crane manufacturing experience and customized engineering capabilities, Henan Mine Crane Factory provides RTG solutions tailored to your yard layout, throughput requirements, and future automation goals.

    Looking for a high-performance RTG crane with advanced anti-sway technology? Contact Henan Mine Crane Factory today to discuss your project and discover how our customized solutions can improve safety, productivity, and long-term operational efficiency.

    Henan Mine CraneDiscuss your requirements ↗
  • How Overhead Cranes Improve Workplace Efficiency

    How Overhead Cranes Improve Workplace Efficiency

    How Overhead Cranes Improve Workplace Efficiency

    In heavy industry, mining, warehousing and logistics, material handling efficiency determines enterprise capacity and competitiveness. As the core industrial lifting equipment, overhead cranes can crack the handling bottleneck by virtue of the advantages of high efficiency, safety and flexibility. This article will analyze the core logic of its efficiency, application and selection, to help enterprises reduce costs and improve production.

    What Is an Overhead Crane

    Overhead Crane, also known as crane, is a kind of lifting equipment running along the top track of the plant or warehouse, the core role is to realize the vertical lifting and horizontal movement of heavy objects, widely used in various industrial scenarios, is to enhance the efficiency of material handling of the core industrial lifting solutions.

    Definition and working principle

    Bridge crane through the bridge across the work area, by the lifting mechanism (hoist), the operating mechanism (trolley, trolley) with the track to achieve the accurate movement of heavy loads in three-dimensional space, the heavy loads from one operating point to another quickly transferred to another operating point, the whole process without the intervention of the ground, to fundamentally solve the traditional material handling cumbersome and inefficient, is to enhance the efficiency of the material handling of the core equipment.

    warehouse lifting equipment

    Key components

    • Bridge: As the main beam of the crane, it carries the weight of the whole equipment and heavy loads. It is welded with high-strength steel to ensure smooth operation and provide basic support for efficient operation.
    • Hoist:The core lifting component, responsible for the lifting and lowering of heavy loads, divided into electric hoist and manual hoist, the industrial scene is mainly electric hoist, Henan Mine Crane Factory supply equipped with high-efficiency motors, the lifting and lowering speed can be flexibly adjusted, significantly improving operational efficiency.
    • Trolley: Drive the hoist along the bridge transverse movement, with the car to achieve a full range of heavy loads covered, running smoothly without lagging, reducing the operating waiting time.
    • Rail: Provide running track for trolley and trolley, adopting high-precision processing technology, easy to install to ensure smooth running of the crane, avoiding the impact of operational efficiency due to rail deviation.

    Common types

    Different industrial scenarios have different needs for cranes, accurate selection is a prerequisite to improve efficiency, Henan Mine Crane manufactured bridge cranes can provide a full range of types.

    • Single girder overhead crane: simple structure, small footprint, load range of 1-20 tons, suitable for small and medium-sized workshops and warehouses, cost-effective, suitable for light and medium-sized material handling, and effectively improve the efficiency of material handling in workshops.
    • Double girder overhead crane: strong load capacity (20-500 tons or more), stable operation, suitable for large-scale mines, iron and steel mills and other heavy-duty scenarios, which can realize efficient continuous operation and crack the problem of heavy-duty material handling.
    • Gantry cranes: can operate outdoors without plant support, suitable for ports, yards, mines and open areas, suitable for large equipment and bulk material handling, to enhance the efficiency of outdoor operations.
    • Jib Crane: Highly flexible, suitable for localized workshop operations, small-scale heavy load transfer, make up for the blind spot of large cranes, and enhance the efficiency of localized material handling.

    Why Workplace Efficiency Matters in Heavy Industry

    For mining, steel, logistics and other heavy industry, efficiency is benefit is not a slogan, inefficient material handling will not only drag down production capacity, but also generate a lot of hidden costs, become a stumbling block to corporate profitability. Combined with the current situation of the industry, the harm of inefficient operation is mainly reflected in three aspects.

    Stricter safety regulations

    Labor costs in the industrial field are rising, and traditional material handling relies on a large number of manual labor, which is costly and inefficient, and difficult to meet the large-scale production. At the same time, industrial safety regulations are tightening, manual handling is easy to cause safety accidents, violations will face high fines and the risk of production stoppage. Bridge cranes can replace manual heavy-duty handling, reducing costs and compliance, and avoiding risks at the source.

    Production delays

    Material handling is the centerpiece of heavy industrial production, and inefficiencies can lead to disconnections. Inefficient material handling can lead to disconnections. Ore transfer in mines does not affect subsequent processing, steel transfer in steel mills lags behind production line stoppages, and slow loading and unloading in warehouses delays logistic deliveries. Long-term accumulation will significantly reduce capacity, increase hidden costs, which is the key reason why enterprises choose bridge cranes.

    Industry bottlenecks

    Mining, steel, logistics is the material handling needs concentrated and inefficient disaster areas. Mining environment is harsh, manual handling of heavy ore inefficient and difficult. Iron and steel mills are characterized by heavy materials and high temperatures, which make it impossible for manual labor and small equipment to transfer efficiently. Warehouse goods in large quantities, turnover, the traditional way easy to congestion. Overhead cranes can accurately solve these pain points and double efficiency.

    8 Key Ways Overhead Cranes Improve Workplace Efficiency

    As a professional Henan Mine Crane manufacturer, we combine our own product research and development experience with thousands of customer application data to summarize 8 key ways to improve workplace efficiency with overhead cranes, each of which has been verified in actual scenarios, and actually helps enterprises to reduce costs and increase production capacity.

    Rapid Material Handling

    Bridge cranes run in a straight line at a high altitude without going around, realizing efficient transfer of heavy materials. Compared with manual or forklift handling, it runs faster and can work continuously, significantly shortening the material handling cycle. Mining enterprises use it to transfer ore, the single transfer time is shortened by more than 60%, and dozens of additional transfers can be completed, which directly improves the efficiency of mining operations and factory productivity.

    bridge crane applications

    Reduce Labor Fatigue

    Traditional heavy-duty handling relies on manual labor, which is labor-intensive, inefficient and prone to errors, Henan Mine Crane Factory overhead cranes can completely replace manual heavy-duty handling, reduce the reliance on forklifts, increase efficiency by 3-5 times compared with forklifts, and liberate workers’ labor. At the same time, it reduces labor input, lowers labor costs, relieves worker fatigue, and indirectly improves overall work efficiency.

    Saving ground space

    Bridge cranes run at high altitude without occupying ground space, which can release the ground for arranging production lines, stacking materials and setting up channels. Compared with ground handling equipment, it can reduce operational congestion, so that handling and production do not interfere with each other, and improve layout efficiency. After the warehouse is used, the floor stacking space increases by 30% and the goods turnover efficiency increases by 40%, highlighting the advantage of space utilization.

    Optimizing workflow

    Henan Mine Crane Factory bridge cranes can be deeply integrated with the production process, realizing seamless material connection and avoiding production linkage. In steel mills, it can transfer steel directly to the casting process, and then transfer molded steel to storage. In mines, it can realize the continuous transfer of ore, avoiding the accumulation of stagnant materials, and guaranteeing a smooth and efficient production process.

    Enhancement of operational precision

    Heavy industrial material handling is prone to collision and loss, the bridge crane is equipped with an accurate control system, with a positioning accuracy of ±1mm, which can avoid material collision and fall and reduce loss and rework costs. Precision equipment handling error control in millimeters, steel transfer can prevent leakage, not only to enhance safety, but also effectively improve the efficiency of material handling.

    Enhance operational safety

    Safety accidents can limit the efficiency of the enterprise, which not only cause casualties, but also lead to work stoppages, resulting in high economic and time loss. Equipped with multiple safety protection devices such as overload limiters and limit switches, overhead cranes can effectively avoid potential safety hazards, and operators can operate remotely or at the control center, away from high-risk areas, to ensure operational safety and stable efficiency.

    Reduced operating costs

    Compared with forklifts and other fuel-powered handling equipment, overhead crane adopts electric drive, which consumes less energy, and one overhead crane can replace several forklifts or manual labor, which greatly reduces the operating cost of the equipment.

    At the same time, our bridge cranes are equipped with energy-saving motors and frequency control systems, which reduce energy consumption by more than 20% compared with traditional cranes. Long-term use of the bridge cranes can save a lot of operating costs for the enterprise, and indirectly improve the profitability and efficiency of the enterprise.

    Adaptation to intelligent production

    With the advancement of Industry 4.0, intelligent manufacturing has become the core direction for enterprises to improve efficiency, and overhead cranes can be deeply integrated with intelligent control systems, sensors, PLC and other equipment to realize semi-automated and fully automated operations. Bridge cranes can realize efficiency improvement in many industrial fields, but in mining, steel, warehousing and logistics, construction prefabrication yard and other scenarios, the efficiency improvement is most significant.

    Industry Applications Where Efficiency Gains Are Highest

    Bridge cranes can achieve efficiency gains in a variety of industries, but are most effective in mining, steel, warehousing and logistics, and construction prefabrication yards.

    Mining Industry

    Mining industry is a core application for overhead cranes, with high material handling volumes, harsh operating environments and high continuity requirements. henan Mine Crane Factory’s overhead cranes can handle ores and large mining equipment, and are suitable for high temperature, dusty and heavy-duty working conditions, realizing 24-hour continuous operation and cracking the handling bottleneck.

    Steel and metal fabrication

    Henan Mine Crane manufactured bridge cranes are precisely adapted to the whole process of steel production, efficiently transferring materials such as molten steel, steel, rolls, etc., avoiding high temperature material loss and guaranteeing operational safety.

    Warehousing and logistics

    The core demand of warehousing and logistics is to quickly complete the loading and unloading, stacking and turnover of goods, and the overhead cranes can be accurately adapted to this scenario. Compared with manual and forklift handling, it can realize overhead stacking, enhance the utilization of warehouse space, avoid operational congestion, and significantly shorten the turnaround time of goods. It can effectively reduce logistics costs, improve logistics time, and highlight the advantages of material handling efficiency.

    Construction and precast yards

    Construction and precast yards material handling is mainly repetitive and heavy-duty, such as steel reinforcement, cement prefabricated parts, large-scale construction equipment, etc., which requires high operational consistency and safety. Overhead cranes can efficiently perform repetitive lifting tasks, reducing labor input, avoiding material damage, and lowering rework costs. They can be used in prefabrication yards to transfer prefabricated parts and in construction sites to transfer large-scale equipment, which can greatly improve the transfer efficiency, shorten the construction period, and ensure the safety and progress of the construction.

    How to Choose the Right Overhead Crane for Maximum Efficiency

    Choosing the right overhead crane is the prerequisite for maximizing efficiency. As a professional manufacturer of mining cranes in Henan, we combine many years of selection experience to provide enterprises with 4 core selection recommendations to help enterprises accurately match the needs to avoid selection errors resulting in efficiency losses and cost waste.

    Load capacity and span requirements

    Need to accurately match the crane type according to the weight of the material, the operating span, the specific points are as follows:

    1. Light and medium-sized materials (1-20 tons), small span operation (6-15 meters): Choose single girder overhead crane, its structure is simple, cost-effective, flexible operation, suitable for small and medium-sized workshops, warehouses and other scenes.
    2. Heavy load materials (more than 20 tons), large span operation (more than 15 meters): Choose double girder overhead crane, with strong loading capacity and stable operation, which can realize efficient and continuous operation, and is suitable for heavy load scenarios such as mines and iron and steel factories.
    3. Outdoor large-span operation: Choose gantry cranes, which do not require plant support, and are suitable for harbor and mine open areas, can efficiently handle large equipment and bulk materials, and are suitable for outdoor harsh working conditions.
    4. Combined with the operating height selection: To avoid the efficiency of the lifting stroke is too long, the lifting height increases by 3-5 meters, the single cycle time may increase by 10%-20%, need to optimize the configuration according to the actual working conditions.

    Working duty classification

    The working duty classification of overhead crane is divided into A1-A8, different levels correspond to different working intensity, the specific points are as follows:

    • Intermittent work: Choose A1-A3 level cranes, suitable for small amount of work, non-continuous operation of the scene, to meet the basic handling needs, to avoid the waste of idle equipment.
    • Continuous operation: Choose A4-A8 class cranes, of which the metallurgical industry casting cranes can work up to A7/A8 class, to ensure the long-term stable operation of the equipment, to avoid equipment fatigue resulting in decreased efficiency or failure.

    Custom attachments

    Different materials have different handling needs, and need to be matched with appropriate customized attachments to enhance operational efficiency. For handling bulk materials, such as ore, coal, etc., the machine can be equipped with grapple attachments to realize batch gripping and fast transfer. For steel and scrap handling, it can be equipped with electromagnetic suction cup attachment to enhance the gripping efficiency. For handling precision equipment, it can be equipped with flexible spreader to avoid equipment damage.Henan Mine Crane manufactured can customize the exclusive attachments according to the specific material types of enterprises, so that the crane can be more suitable for the operational needs, and further enhance the efficiency.

    industrial crane

    Indoor or outdoor application needs

    For indoor applications such as workshops and warehouses, single girder and double girder overhead cranes can be selected without considering the environmental impacts of wind, rain and sand. For outdoor application such as mine open area, harbor, etc., gantry cranes or outdoor type overhead cranes should be selected, with rain cover and windproof anchoring devices, to adapt to the harsh outdoor environment, to ensure the stable operation of the equipment, and to avoid the influence of environmental factors on the operational efficiency.

    Common Mistakes That Reduce Crane Efficiency

    Many enterprises are equipped with overhead cranes, but due to improper operation, selection and maintenance, the efficiency of the crane can not be fully utilized, and even efficiency decline, frequent failures and other problems. The following summarizes the 4 common misunderstandings, to help enterprises avoid the risk.

    Selecting the wrong crane type

    Some companies blindly pursue low prices, choose the load capacity, work level is not enough crane, resulting in the crane can not carry heavy materials, or can not meet the demand for continuous operation, frequent failures, but reduce efficiency. There are also some enterprises choose too large load, too high working level of the crane, resulting in idle equipment, energy waste, increase operating costs.

    Poor workshop layout planning

    Crane track layout, work area planning, directly affecting operational efficiency. Part of the enterprise workshop layout confusion, track setup is unreasonable, resulting in crane running obstruction, detour, increase operating time. At the same time, the ground materials are stacked haphazardly, occupying the crane operating space, will also reduce operational efficiency.

    Lack of operator training

    The operation of overhead cranes requires professional skills, if the operator is not trained systematically, the operation is not skilled, not standardized, which will lead to slow operation speed, inaccurate positioning, and even operational errors, causing safety accidents and affecting operational efficiency.

    Ignoring routine maintenance

    The core components of overhead cranes require regular maintenance. Ignoring routine maintenance will lead to wear and tear of the components, frequent failures, and increased downtime of the equipment, which directly affects the work efficiency. For example, wire rope without regular lubrication will lead to increased wear and tear, shorten the service life, and even lead to breakage accidents. The motor is not regularly serviced, which will lead to a decrease in operating efficiency and an increase in energy consumption.

    Henan Mine Crane Factory Custom

    As an industrial core lifting equipment, overhead crane relies on core components to realize efficient transfer of heavy loads, and is suitable for many types of industrial scenes, which can effectively crack the bottleneck of material handling in heavy industry, and improve operational efficiency, reduce costs and ensure safety through various ways, and is suitable for the development trend of intelligence. Reasonable selection, avoid common misunderstandings, in order to give full play to its value, help enterprises to improve production capacity, enhance core competitiveness, is an important support for heavy industry to reduce costs and improve production.

    As a company with years of experience in the industry, Henan Mine Crane Factory focuses on the research, development, production, and sales of high-quality bridge cranes. We can provide customized industrial lifting solutions based on your specific needs, ensuring that equipment maximizes work efficiency and helps your company reduce costs and expand production capacity.

    Upgrade your production facilities immediately, choose the reliable Henan Mine Crane Factory to unlock new possibilities of efficient production and give your enterprise an edge in the industry competition!

    Henan Mine CraneDiscuss your requirements ↗