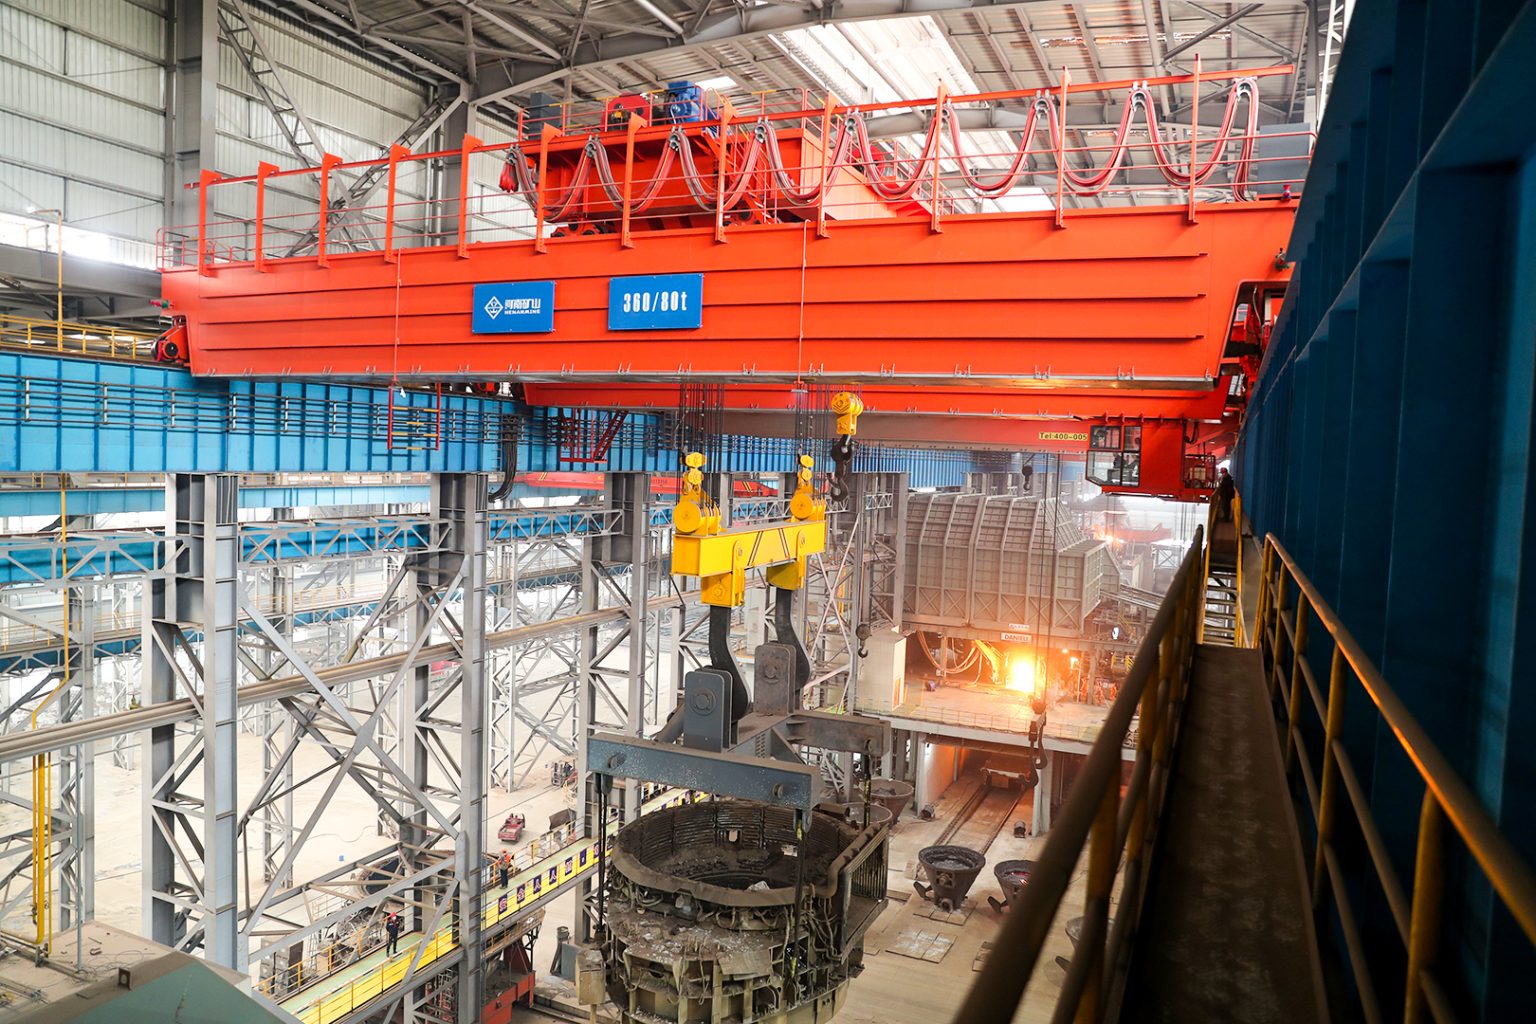
Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

作者: YUWEI, YUWEI

  • Explosion-Proof Gantry Crane & Overhead Crane for Industrial Hazardous Zones

    Explosion-Proof Gantry Crane & Overhead Crane for Industrial Hazardous Zones

    Explosion-Proof Gantry Crane & Overhead Crane for Industrial Hazardous Zones

    Explosion-proof cranes and ordinary industrial cranes may look similar in appearance and structure, but the core design, accessory configuration, safety logic and compliance standards are completely different. Choosing the wrong model will not only lead to equipment can not pass the project acceptance, but also leave continuous safety hazards.

    This article combines various types of industrial high-risk projects around the world landing experience, a clear comparison of the two types of Crane application scenarios, core differences, selection parameters, pit avoidance points, to help purchasers accurately match the appropriate equipment.

    Mainstream application project scenarios of the two types of Cranes

    Explosion-proof cranes and ordinary cranes are very clear application boundaries, whether or not there is a source of explosive hazards within the scene, is the core premise of the distinction between the selection of different scenarios of the risk level and equipment fitness standards are significantly different.

    Oil and gas facilities

    Oil and gas mining and processing plants belong to the first-class high-risk explosion-proof scene, the operation area is always present in the spread of combustible gas leakage risk. Equipment overhaul, pipeline lifting, heavy equipment shifting and other operations, the whole process needs to eliminate any ignition source.

    This type of scene is strictly prohibited the use of ordinary Crane, must be equipped with compliant explosion-proof lifting equipment, the whole control of electrical sparks, mechanical friction sparks, suitable for oil and gas mixture of high-risk explosive environment.

    Chemical and petrochemical plants

    Petrochemical deep processing, fine chemical plant will store, process all kinds of flammable and explosive solvents, process gases and chemical raw materials. Production process volatile vapors, diffuse harmful gases, will make the workshop in a long-term unstable high-risk state.

    Tanks, equipment and material lifting operations in the workshop must use chemical-specific explosion-proof Crane to meet the explosion-proof compliance requirements of the hazardous area and avoid safety accidents caused by equipment operation.

    Spraying and solvent treatment workshop

    Paint, coating, solvent storage workshop air, will continue to float in the low-flashpoint volatile vapors. These media are extremely sensitive, and the slightest electrical spark, or high temperature surface of equipment, can trigger a risk of combustion or explosion.

    All lifting equipment into the operating area, need to have explosion-proof attributes, to eliminate the common electronic control, mechanical structure of the safety hazards.

    Grain and oil, powder processing plant

    Flour, feed, sugar, starch and other powder processing, will produce a large number of fine suspended dust. After the dust gathering reaches a certain concentration, a dust explosion environment will be formed, which is a typical solid high-risk explosion-proof scenario.

    Raw material transfer, equipment maintenance, finished product lifting dust explosion-proof Crane, need to be targeted to do a good job of dust sealing, electrostatic discharge, temperature control protection, different from ordinary industrial lifting equipment.

    Coal, carbon black powder plant

    Coal processing, carbon black production, powder transfer stations, high dust concentration, accumulation speed, and high frequency of equipment operations, mechanical friction, electrostatic buildup of risk is prominent.

    This kind of dust high-risk areas, must use explosion-proof cranes suitable for dust conditions, the open structure of the ordinary Crane is very easy to accumulate dust, sparks, can not meet the requirements of safe production.

    Ordinary plants and conventional warehouses

    Ordinary production workshops, finished product warehouses and logistics yards without flammable and explosive media and without the risk of dust accumulation belong to the conventional industrial environment. The operation process will not produce explosive atmosphere, no ignition source control just need.

    This kind of scene does not need high-matching explosion-proof equipment, regular Overhead C ranes and Gantry Cranes can fully meet the lifting needs, more cost-effective, more convenient operation and maintenance.

    how to choose explosion-proof crane

    Core operational requirements of hazardous area projects

    The core of lifting operations in high-risk scenarios is not to improve lifting efficiency, but to avoid the risk of explosion in all aspects. All the equipment selection, operation specification, operation and maintenance standards, are centered on the control of hazardous sources.

    All-round control of ignition sources

    The core cause of industrial explosion is all kinds of controllable ignition sources, including electrical sparks generated by the start and stop of electrical fittings, mechanical sparks generated by the friction and collision of equipment, high temperature surfaces formed by long-term operation, and accumulation of static electricity.

    All the design optimization of Ex cranes used in hazardous areas revolves around the elimination of ignition sources, eliminating potential safety hazards from the structural and accessory levels.

    Equipment adapted to the risk of real working conditions

    You can’t define the type of equipment based on the industry of the plant alone, and the same plant will be divided into hazardous and safety zones. Part of the chemical plant office, warehousing area without high-risk media, no explosion-proof equipment; while the production process area must be strictly adapted to explosion-proof models.

    The core of the selection is the real environment of the equipment operating point, rather than the overall industry attributes of the plant.

    Distinguish between gas risk and dust risk scenarios

    Gas explosion-proof and dust explosion-proof are two completely independent systems, protection structure, certification standards, design logic are different. Gas scenarios focus on electrical sealing, spark prevention and control, dust scenarios focus on dust, temperature control, static electricity export.

    Mixed use of equipment can lead to protection failures, which is the main reason why many projects fail acceptance and leave hidden safety hazards.

    Take into account the practicality of equipment operation and maintenance

    Explosion-proof equipment can not only pursue the level of protection, excessive closure, structural complexity of the protection design, will significantly increase the difficulty of daily maintenance, parts replacement.

    Qualified hazardous area Crane, will be under the premise of safeguarding explosion-proof safety, set aside a reasonable space for operation and maintenance, suitable for long-term normalized operation and maintenance needs.

    Complete compliance qualifications and technical documents

    Global high-risk industrial projects, explosion-proof equipment is extremely strict compliance audit. Equipment must have the corresponding level of explosion-proof certification, exclusive marking, a full set of technical drawings and accessories compliance documents.

    These materials are the core basis for project acceptance, compliance filing, overseas customs clearance, ordinary Cranes do not have such qualification documents.

    Long-lasting spare parts and exclusive after-sales protection

    The spare parts of explosion-proof equipment are exclusive customized models, which can not be common with ordinary Crane spare parts. The risk of equipment downtime in high-risk scenarios is extremely high, requiring manufacturers to provide a long-term stable supply of spare parts and professional after-sales guidance.

    The basic definition of the two types of Crane and the applicable scenarios

    Many purchasers can not accurately distinguish between the core positioning of the two types of equipment, in short, ordinary cranes serve regular industrial scenes, explosion-proof cranes exclusive of various types of high-risk hazardous areas.

    What is explosion-proof Crane?

    Explosion-proof Crane is a special lifting equipment specially designed for explosive hazardous environments, the entire machine from the motor, electronic control, cable, braking system to the mechanical friction structure, all using explosion-proof exclusive configuration.

    The equipment can effectively inhibit electrical sparks, mechanical sparks, high temperature surfaces, static buildup and other ignition sources, suitable for gas, steam, dust and other types of high-risk explosive environments, fully meet the ATEX, IECEx and other global explosion-proof compliance standards.

    What is an ordinary Crane?

    Ordinary industrial cranes are conventional general-purpose lifting equipment, only to meet the basic lifting, transfer, overhaul functions. Equipment accessories, electronic control system, mechanical structure are general industrial configuration, without any explosion-proof protection design.

    Prioritize the use of explosion-proof Crane scenes

    Work area perennial or intermittent combustible gases, volatile vapors, suspended combustible dust, the formation of explosive atmosphere conditions. Equipment running track, operating range covering the calibrated hazardous area, need to enter the high-risk areas throughout the operation.

    The local supervision of the project requires the equipment to have Ex explosion-proof certification, hazardous area compliance qualification, such scenes must be a full set of explosion-proof lifting equipment.

    Ordinary Crane is fully adequate for the scene

    The factory area has been professionally surveyed, is a non-hazardous ordinary area, normal production operations will not produce any explosive gas or dust atmosphere. Equipment throughout the safe area operation, will not enter any calibration of high-risk areas.

    Conventional warehousing, machining, assembly workshop and other non-explosion-proof requirements of the working conditions, the choice of ordinary Crane more cost-effective, fully meet the production requirements.

    Adaptation program for mixed working conditions

    Many large factories exist in the working conditions of the partition, the safety of the region using ordinary cranes to complete routine operations, only high-risk process areas, maintenance points configured with explosion-proof lifting equipment, partition adaptation, according to the need for selection, balancing safety and cost.

    Part of the project does not require the entire machine explosion-proof, only the electronic control, motor and other core spark-prone components need explosion-proof configuration, can be used with ordinary Crane local explosion-proof accessories customized solutions.
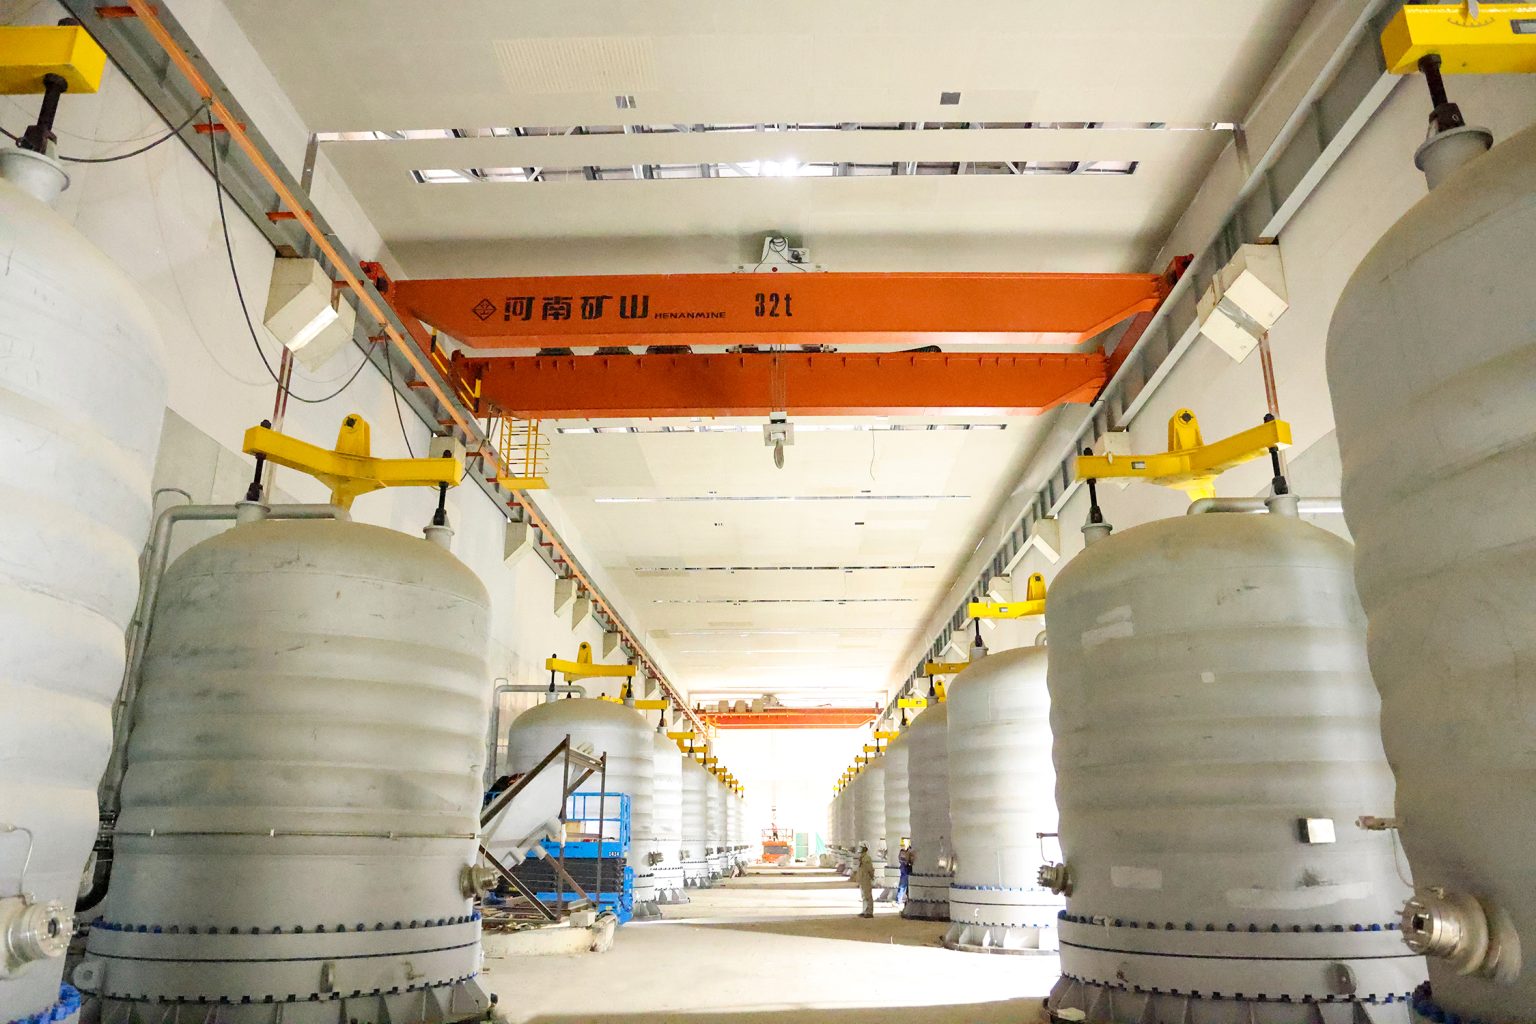
    how to choose explosion-proof crane

    Core differences between explosion-proof cranes and ordinary cranes

    The appearance of the two types of equipment, lifting function similarity is very high, but the core design, safety standards, adaptable working conditions have essential differences, but also procurement selection must focus on checking the content.

    Applicable working conditions are different

    Explosion-proof Crane is designed for various types of hazardous areas, can be adapted to oil and gas, chemical industry, painting, powder and other flammable and explosive high-risk scenarios, can be in the high temperature, dust, corrosive, explosive and stable operation of complex environments.

    Ordinary Cranes are only adapted to regular room temperature, no flammable and explosive media, no high-strength dust in ordinary industrial environments, can not withstand the safety risks of high-risk working conditions.

    Different configurations of core parts

    All core accessories of explosion-proof Cranes are exclusive explosion-proof models, including explosion-proof motors, explosion-proof brakes, explosion-proof limit switches, sealed electronic control boxes, flame retardant explosion-proof cables, explosion-proof operating handles and remote control systems.

    All electrical and mechanical components that are prone to sparks and high temperatures are designed with explosion-proof modifications. Ordinary Cranes use common industrial parts without any sealing, flame retardant, explosion-proof optimization treatment.

    Ignition source control capability is different

    The core of explosion-proof Crane design is to eliminate all potential ignition sources, through the sealing of explosion-proof, safety protection, intrinsic safety design, electrostatic discharge, material optimization and other ways to eliminate sparks and high temperature generation.

    Ordinary Crane has no ignition source control design, equipment start and stop, friction, electrical failure process, it is very easy to produce electrical sparks and mechanical sparks, in high-risk environments will directly lead to safety accidents.

    Compliance certification requirements are different

    Explosion-proof Crane is a special compliance equipment, must pass the professional explosion-proof testing, hold the corresponding regional explosion-proof certification, working condition suitability certificate, equipment level marking, supporting complete technical documents, to meet the acceptance criteria for all types of high-risk projects around the world.

    Ordinary Cranes only need to meet the basic industrial lifting equipment standards, without explosion-proof certification and compliance information, the entry threshold is lower.

    Different equipment cost

    Explosion-proof Crane’s customized accessories, explosion-proof structural design, compliance testing process, exclusive process standards, will increase production costs, the overall offer is much higher than the same tonnage, the same span of ordinary Crane.

    Ordinary Crane mass production of high degree, common accessories, simple process, procurement costs and lower landed costs, suitable for regular working conditions batch selection.

    Different maintenance standards and difficulties

    Explosion-proof Crane maintenance requirements are more stringent, you must use the original explosion-proof special parts, overhaul process, replacement cycle, operating norms have clear standards, improper maintenance will directly damage the explosion-proof performance of the equipment.

    Ordinary Crane maintenance process is simple, strong generality of accessories, conventional factory operation and maintenance personnel can complete the daily maintenance and replacement of accessories.

    Selection decision logic is different

    Professional selection will not be based on experience or subjective preference for equipment, but the site hazardous area survey report, the type of hazardous sources, the scope of operation as the core basis. Eliminate the risk of under-matching and avoid the cost waste caused by blindly over-matching.
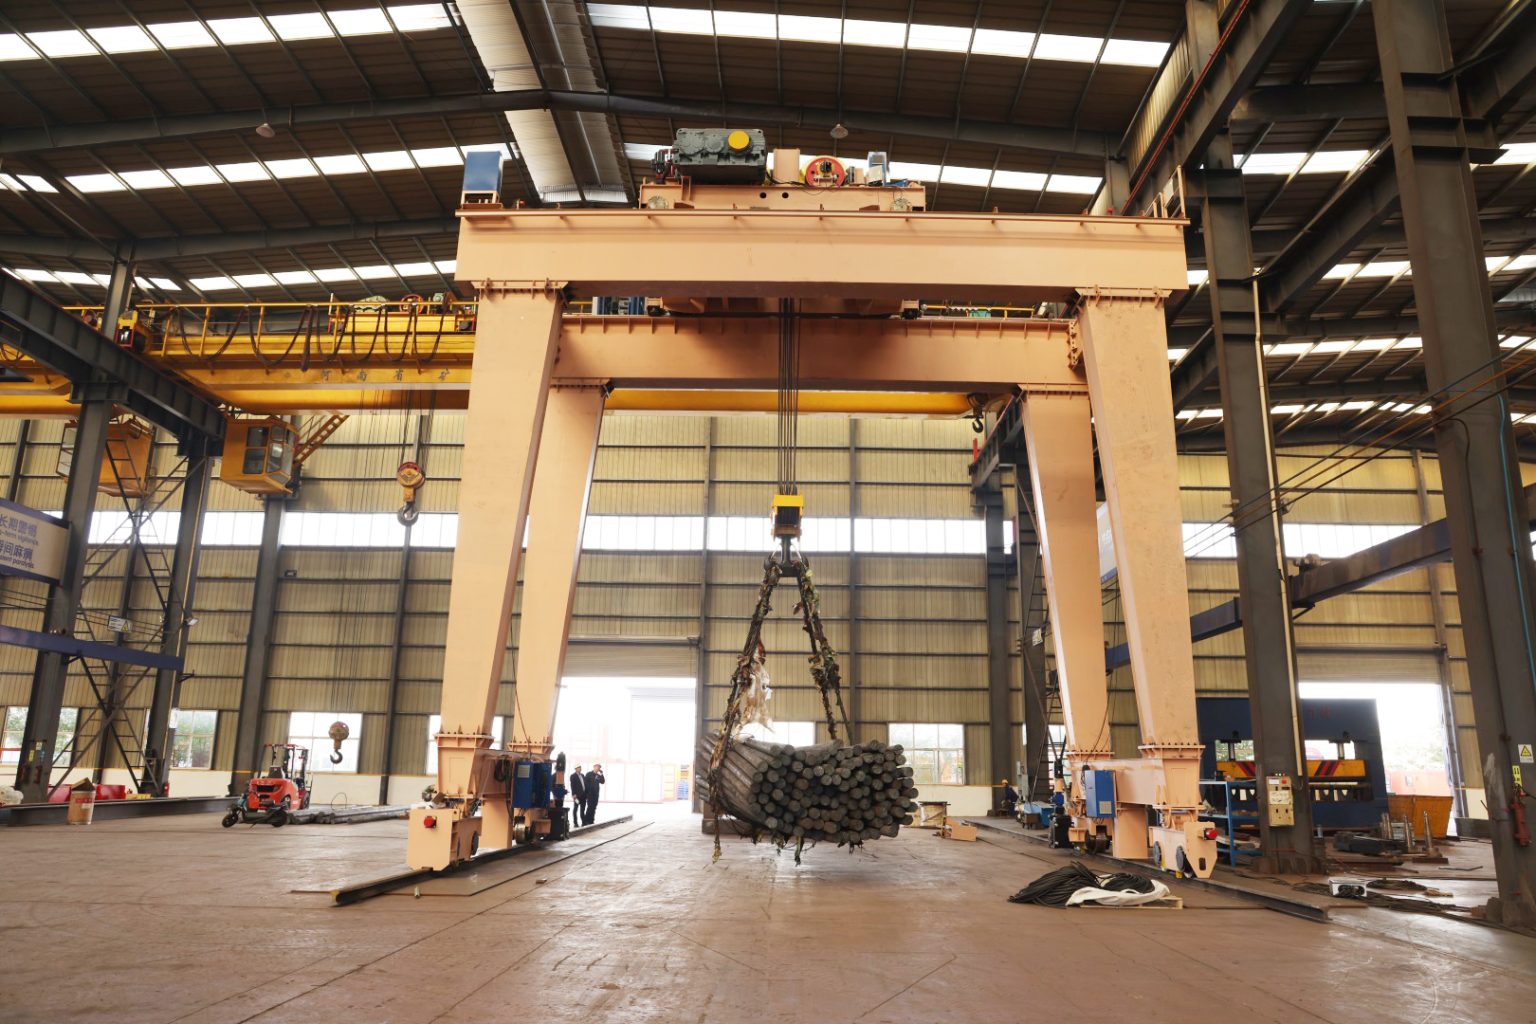
    how to choose explosion-proof crane

    Core technical parameters that must be verified for procurement

    No matter which model you choose, you need to check the core parameters with the project conditions to ensure that the equipment is suitable for the production needs and meets the compliance standards at the same time.

    Hazardous source type

    Make it clear whether the site is a single source of gas, vapor, mist, dust, or a mixed source of gas and powder. Different hazardous sources correspond to different explosion-proof standards, which directly determines the direction of equipment selection.

    Hazardous area level

    Check the project survey labeled area properties, distinguish ordinary non-hazardous areas, gas 0/1/2 area, dust 20/21/22 area, the equipment protection level must accurately match the area level.

    Rated lifting tonnage

    Calculate the tonnage according to the self-weight of the lifted goods, the weight of the spreader, the maximum operating load, and reserve a reasonable load margin to avoid long-term full-load operation affecting the stability of the equipment.

    Equipment span

    Strictly match the center distance of the workshop track, plant layout and operation coverage to ensure the smooth operation of the equipment, no blind zone, and adapt to the site civil construction conditions.

    Effective lifting height

    Combined with the equipment lifting path, cargo stacking height, plant floor height, and safety spacing to determine, to meet the height requirements of daily production lifting and equipment maintenance.

    Working level

    Differentiate the use of equipment, whether it is low-frequency equipment maintenance lifting or high-frequency normalized production lifting, different operation frequency corresponds to different equipment working level, to ensure the durability of equipment.

    Environmental conditions

    Comprehensively consider the site environment temperature, equipment surface temperature control needs, humidity, dust accumulation, corrosive media and other factors, targeted optimization of equipment protection configuration.

    Equipment control mode

    High-risk hazardous areas are prioritized to use wireless remote control to reduce the risk of personnel working in close proximity; common areas can choose handle control, cab control and other conventional modes.

    Mechanical risk point protection

    Focus on verifying the protection design of brakes, traveling wheels, transmission friction points and metal contact parts to avoid mechanical friction sparks and high temperature risks.

    Electrical protection principle

    Clarify the electrical protection mode of the equipment, confirm that the protection design is suitable for the hazardous working conditions at the site, meet the local explosion-proof compliance requirements, and ensure long-term stable operation.

    Reliable Crane Supplier Screening Criteria

    Ordinary Crane manufacturers can not land the customization and production of explosion-proof equipment, high-risk project selection of suppliers, focusing on verification of industry-specific experience and landing capacity.

    Verification of hands-on experience in hazardous area projects

    Priority is given to manufacturers with a large number of explosion-proof project landing experience, as distinguished from manufacturers who only produce ordinary Cranes. Manufacturers must be familiar with the design standards and compliance requirements for all types of gas and dust high-risk conditions.

    Verification of similar industry landing cases

    Focus on checking the manufacturers in the oil and gas, chemical, coating, grain and oil powder, new energy and other high-risk industries, real project cases, to verify the suitability of equipment conditions and project landing capacity.

    Evaluation of professional engineering adaptability

    High-quality manufacturers will take the initiative to determine whether the project needs explosion-proof equipment according to the customer site conditions, distinguish between explosion-proof and local explosion-proof, to give a cost-effective cost-effective selection of the project, rather than simply promote the high allocation of equipment.

    Verification of a full set of professional and technical information

    Regular manufacturers can provide a full set of equipment assembly drawings, electrical schematics, explosion-proof marking instructions, compliance certificates, core accessories parameters, operating manuals and other information to meet the global project acceptance requirements.

    Confirmation of core component brands and compliance

    Verify the brands and explosion-proof qualifications of explosion-proof motors, brakes, limit switches, electronic control systems, cables, operating accessories, and all core accessories must be compliant with the standards, and eliminate low-match replacement.

    Clarify the scope of testing and commissioning services

    Confirm the manufacturer’s factory testing, performance testing, on-site installation guidance, machine commissioning, personnel training and other services, to ensure that the equipment can be put into production in a compliant manner after entering the field.

    Verify compliance coverage

    Confirm in advance whether the equipment is the whole machine explosion-proof compliance, or local accessories explosion-proof adaptive, matching the project regulatory requirements, to avoid non-compliance with the scope of compliance leading to acceptance failure.

    Verification of after-sales and spare parts protection

    Exclusive accessories for explosion-proof equipment with poor generality, manufacturers need to have long-term spare parts inventory, fast after-sales response, remote operation and maintenance guidance capabilities to reduce equipment downtime losses.
    how to choose explosion-proof crane

    Procurement selection of common misconceptions

    Many of the project’s safety hazards and cost waste, are derived from the cognitive bias in the procurement stage, these high-frequency misunderstandings can be effectively avoided.

    Mistakenly believe that all industrial plants need explosion-proof Crane, blindly high allocation of equipment, significantly increasing the project procurement costs.

    Luck, in the calibration of the dangerous area using ordinary Crane, direct contact with the red line of production safety, buried a major explosion hidden danger.

    Confuse gas explosion-proof and dust explosion-proof conditions, misallocation of equipment types, resulting in equipment protection failure.

    Simply select the type at a low price, ignoring the qualification of equipment compliance and quality of accessories, the equipment can not pass the project acceptance.

    Blindly over-selecting equipment without verifying the real source of hazards on site, resulting in redundant equipment performance and wasted budget.

    Unable to accurately determine the operating range of the equipment, mistakenly classified ordinary equipment into the hazardous area operation.

    Only verify the explosion-proof qualification of the whole machine, ignoring the compliance of the core parts, and there are protection loopholes.

    Failure to plan in advance for long-term maintenance and spare parts replacement program, equipment later explosion-proof performance gradually failed.

    Frequently Asked Questions

    What is the core difference between explosion-proof cranes and ordinary cranes?

    The core differences between the two focus on design logic, parts configuration, safety protection and applicable working conditions. Ordinary cranes only meet the basic lifting function, no explosion-proof design; explosion-proof cranes from the machine structure, electrical systems, mechanical components, all-round avoidance of ignition sources, exclusively adapted to the flammable and explosive hazardous areas, and have formal explosion-proof compliance qualifications.

    All high-risk areas must use explosion-proof Crane?

    No. Only the labeled hazardous areas need to use explosion-proof cranes. Only standardized hazardous areas require explosion-proof equipment, ordinary storage, office, non-process areas in the plant, no explosive media and atmosphere, the use of ordinary cranes can be, without the need for mandatory high matching.

    Can ordinary Crane be used around the hazardous area?

    If the equipment is running in the safe area throughout the whole process, the operation range and operation track will not enter the hazardous area, and will not contact with high-risk media, ordinary Cranes can be used normally. Once the operation track covers the hazardous area, the explosion-proof equipment must be replaced.

    Explosion-proof Crane purchase price must be higher?

    With the same tonnage and the same span, the cost of explosion-proof Crane is generally higher than that of ordinary Crane. Exclusive explosion-proof accessories, modified design, compliance testing, and customized processes all add to the production cost, but the safety value and compliance they bring cannot be replaced by ordinary equipment.

    What project information needs to be provided to the manufacturer before requesting a quotation?

    You need to provide the industry you belong to, the type of hazardous source on site, the grade of hazardous area, the required tonnage of the equipment, span, lifting height, operating conditions, the location of the project and the drawing of the plant, so as to facilitate the manufacturers to accurately judge the model and match the compliance program.

    How to determine whether the operation area is a hazardous area?

    It can be determined based on the project’s professional safety survey report, plant area demarcation markings, and the properties of the production medium. Areas where there are combustible gases, volatile vapors, combustible dusts and explosive atmospheres may be formed are high risk hazardous areas.

    Can the same manufacturer provide both ordinary cranes and explosion-proof Cranes?

    Professional lifting equipment manufacturers can provide one-stop general industrial cranes and a full range of explosion-proof cranes to meet the operational needs of the plant zoning, unified equipment standards and after-sales system to reduce the cost of operation and maintenance of the project.
    how to choose explosion-proof crane

    Summarize

    Explosion-proof cranes and ordinary cranes selection, the core basis is always the site of the real working conditions, rather than purchasing habits, project name or subjective perception. There is no absolutely better equipment, only more suitable for the project model.

    Purchasers need to accurately distinguish between ordinary work areas and high-risk hazardous areas, identify the type of gas and dust hazards, and then match the corresponding Crane models, technical parameters and compliance standards, neither risky low matching, nor blindly high matching.

    Reliable equipment suppliers can not only provide compliant lifting equipment, but also with rich global project experience, to provide customers with working conditions assessment, selection guidance, compliance docking, installation and commissioning, long-term operation and maintenance of the whole process of services, to ensure that the project is safe to land, long-term stable operation.

    Henan Mine Crane manufactured industrial lifting equipment for many years, can provide one-stop general industrial cranes, a full range of explosion-proof cranes, suitable for oil and gas, chemical, powder, grain and oil, new energy and other types of domestic and international projects conditions, to meet the ATEX, IECEx and other global compliance standards.

    Not sure whether to choose explosion-proof cranes or ordinary cranes for your project? Provide your industry conditions, hazardous area information, equipment parameters and project drawings, our professional engineering team will customize an accurate and suitable selection plan for you.
    Henan Mine CraneDiscuss your requirements ↗
  • Explosion-Proof Crane Selection Guide | Gas & Dust Hazardous Area Rules

    Explosion-Proof Crane Selection Guide | Gas & Dust Hazardous Area Rules

    Explosion-Proof Crane Selection Guide | Gas & Dust Hazardous Area Rules

    The core logic of explosion-proof level selection is never to benchmark against the highest standards, but to match the real hazardous working conditions on site. Flammable and explosive gases, vapors, mist environment, and combustible dust environment hazard classification, protection logic is completely different, can not apply the same set of selection criteria.

    This paper combines the global ATEX, IECEx, NEC and other mainstream explosion-proof system standards, dismantling various types of explosion-proof scenarios, industry needs, selection logic, core parameters, supplier screening points and procurement of common problems.

    Need to configure explosion-proof equipment for industrial scenes

    Explosion-proof lifting equipment and explosion-proof electromechanical equipment are widely used in high-risk industrial scenarios where flammable and explosive media exist. Different scenes of different hazardous properties, the corresponding explosion-proof equipment level selection criteria will be differentiated adjustment.

    Oil and Gas Facilities

    Oil, natural gas mining and processing plants, there is always the risk of flammable gas leakage, air and oil mixed with explosive atmosphere is very easy to form. Lifting operations, equipment operation and maintenance operations in such scenes require the use of explosion-proof equipment throughout the compliance.

    Explosion-proof cranes, explosion-proof hoists, explosion-proof motors, and explosion-proof control systems in the plant are the core equipment for avoiding explosions caused by electrical sparks and mechanical friction sparks, and they are also the mandatory standard equipment for safe production in oil and gas projects.

    Chemical and petrochemical plants

    Fine chemical and petrochemical deep-processing plant will use a large number of solvents, process gases, volatile raw materials. The vapor and mist generated during the production process will be dispersed in the air of the workshop, forming a continuous or intermittent hazardous environment.

    Material handling, equipment maintenance, finished product lifting operations in the workshop, must use the corresponding level of chemical explosion-proof lifting equipment, to prevent the ignition source generated during the operation of the equipment.

    Painting and solvent treatment workshop

    Painting, spraying, solvent storage and processing workshop, volatile combustible vapors floating in the air all year round. This kind of medium has low ignition point and strong diffusivity, slight electrical spark or high temperature surface may cause safety accidents.

    Workshop lifting equipment, mobile lifting tools, electronic control devices, all need to adapt to the explosion-proof standards of the steam hazardous scene, suitable for intermittent high-risk work conditions.

    Grain, oil and food powder processing plant

    Flour, feed, sugar, starch and other food powder processing, will produce a large number of fine combustible dust. After the dust is suspended and piled up, it is very easy to form a dust explosion environment, which belongs to the typical dust high-risk explosion-proof scenario.

    The lifting equipment used for raw material handling, finished product stacking and equipment maintenance needs to be adapted to the dust explosion-proof standard, focusing on dust-proof sealing, surface temperature control and static electricity prevention and control design.

    Coal and powder material processing plant

    Coal, carbon black, ore powder processing plant, dust concentration is high, the accumulation rate is fast, mechanical friction, electrical failure, electrostatic buildup may induce dust explosion.

    This type of scenario requires higher friction prevention and control, dustproof ability and surface temperature control of the equipment, and ordinary gas explosion-proof equipment cannot meet the safety specifications of the powder plant.

    Pharmaceutical and fine chemical workshop

    Pharmaceutical workshops and fine chemical production scenarios, will frequently use low-flammability solvents and ultra-fine powder raw materials. The workshop environment is highly confined, the media diffusion range is concentrated, and the hazardous atmosphere is controllable but the risk of high precision.

    Equipment selection needs to take into account the requirements of clean production and explosion-proof safety standards, the choice of fine protection of explosion-proof equipment, adapted to a small range of high-risk work environment, high precision.

    Battery and new material production workshop

    Lithium materials, new energy powders, high-end new materials production process, the simultaneous existence of solvent vapors and ultra-fine powder double source of danger, belonging to the rare mixed hazardous working conditions.

    This type of scene can not be applied alone gas explosion-proof or dust explosion-proof standards, need to be combined with dual-risk customized adaptive solutions, but also a composite explosion-proof equipment selection of key difficult scenes.

    explosion-proof crane for different scenarios

    Different high-risk scenarios of the core selection requirements

    The suitability of explosion-proof equipment, depending on the existence of on-site hazardous sources, diffusion range, medium properties. Different scenes of the core protection focus is completely different, can not be uniformly applied to a set of selection criteria.

    Gas, steam, fog high-risk environment

    The core of the danger of this type of scene is the explosive atmosphere formed by combustible gases mixed with air. Risk level by the frequency of the existence of dangerous atmosphere, the duration of the decision, corresponding to the ATEX standard 0 zone, 1 zone, 2 zone gas hazard classification.

    Equipment selection does not need to be blindly high, but only to match the actual working conditions of the site level. Continuously exist in the dangerous atmosphere of the region to choose a high level of protection, and occasionally appear abnormal working conditions in the region, can be adapted to the conventional explosion-proof level, to avoid a waste of resources.

    Combustible dust high-risk environment

    The mechanism of dust explosion and gas explosion is completely different, dust will be suspended to form an explosive cloud, but also in the accumulation of equipment on the surface to form the risk of secondary explosion. The corresponding ATEX 20, 21, 22 dust classification standards, and gas zoning can not be common.

    Dust scenarios focus on the protection of the whole machine dust sealing, surface temperature control, electrostatic discharge, rather than purely electrical explosion-proof, which is also the key point of many procurement selection is prone to error.

    Reliable ignition source control

    High-quality explosion-proof Cranes and ancillary equipment, from the structure, accessories, electronic control, materials, multi-dimensional avoidance of ignition risk, suitable for complex and high-risk working conditions.

    Fit the actual process conditions of the safety design

    Many factories will be labeled with a clear level of hazardous areas, but the actual production process, ventilation conditions, the scope of work there will be slight differences. Equipment selection can not only against the area labeling, to fit the real workflow.

    For example, some marginal areas are labeled as Zone 2, but high concentrations of combustible media can occur briefly during abnormal production, requiring a moderate increase in equipment protection redundancy to ensure safety in extreme working conditions.

    Complete Compliance and Technical Documentation

    Industrial high-risk projects around the world require equipment to be provided with complete explosion-proof certificates, rating labels, construction drawings, and technical specifications. Different countries have different compliance systems, and the suitability of qualification documents directly affects project acceptance.

    Regular manufacturers will support a full set of compliance information to meet the ATEX, IECEx, NEC and other regional project audit standards.

    Long-term maintenance and operation and maintenance adaptability

    Explosion-proof equipment protection performance, rely on long-term standardized maintenance. If the design of the protective structure is too closed and complex, it will increase the difficulty of daily inspection and parts replacement.

    High-quality explosion-proof equipment will protect the protective performance of the premise, set aside a reasonable space for maintenance, so that daily operation and maintenance can be efficient landing, long-term maintenance of explosion-proof equipment performance.

    Standardized explosion-proof grade selection logic

    There is no fixed formula for explosion-proof selection, but there is a standardized landing process. Follow the scientific steps selection, not only to avoid safety risks, but also maximize the control of equipment procurement and operation and maintenance costs.

    The first step: distinguish between the source of danger for gas or dust type

    This is the selection of the most basic and most critical step. Gas, steam, mist scene for 0/1/2 gas explosion-proof system, combustible dust scene for 20/21/22 dust explosion-proof system, the two sets of system protection structure, certification standards, equipment parameters are not interoperable.

    Mixed selection standards, light equipment adaptation failure, heavy leaving major safety hazards, but also the industry’s most common selection errors.

    Step 2: Confirm the site hazardous area level

    Hazardous area rating is based on the frequency and duration of explosive atmosphere. 0 zone, 20 zone for the continuous presence of high-risk atmosphere, 1 zone, 21 zone for normal operations occasionally, 2 zone, 22 zone for abnormal working conditions for a short period of time.

    Accurate approval of the regional level, in order to match the corresponding protection level of high-risk area equipment, to achieve a balance between safety and cost.

    Step 3: distinguish between electrical and mechanical explosion-proof equipment properties

    Explosion-proof equipment is divided into electrical explosion-proof and mechanical explosion-proof two plates. Motor, electronic control, switch, remote control belongs to the electrical explosion-proof category, wheels, brakes, wire rope, friction structure belongs to the mechanical explosion-proof category.

    Different equipment focuses on different explosion-proof, some scenes need to meet the electrical and mechanical dual explosion-proof, a single dimension can not meet the production safety requirements.

    Step 4: Match the corresponding protection program according to the scene

    Different hazardous scenarios correspond to the exclusive protection concept, without the need to pursue the highest level of explosion-proof. Continuous high-risk core process area, the choice of high-standard full protection equipment; edge of the intermittent hazardous areas, the choice of basic compliance protection equipment can be.

    Scientific selection is to match the needs, rather than blindly high matching, which is the core principle of industrial explosion-proof selection.

    Step 5: check the project’s local compliance system

    There are differences in explosion-proof compliance standards in different regions of the world, the mainstream of the European Union using the ATEX system, the international general IECEx system, the North American NEC/CEC system, the scope of certification, labeling requirements, acceptance criteria vary from region to region.

    Selection needs to confirm the project in advance of the local standards, to ensure that the equipment certification, technical documents, marking specifications fully adapted to the local acceptance requirements.

    Step 6: Approved regional classification attributes

    Part of the plant will exist in ordinary areas, conventional hazardous areas, special control of the division of hazardous areas. Special control areas will have additional temperature, static electricity, airtightness requirements.

    Equipment selection must be based on the site of the professional regional assessment report, can not be referred to the business publicity rhetoric or general equipment parameters.

    explosion-proof crane for different scenarios

    Typical industrial scenarios selection differences

    Different high-risk scenarios have different sources of risk, and the focus of equipment selection and protection configuration varies greatly. Combined with the characteristics of the mainstream industrial scenarios, you can quickly lock the appropriate explosion-proof program.

    Oil and gas process production area

    Oil and gas plants are mainly gas explosion risk, mostly divided into 0, 1, 2 gas hazardous areas. The core risk is the dispersion of flammable gas leakage, the explosion-proof level of electrical equipment, sealing, spark prevention and control requirements are extremely high.

    Selection focus on checking the equipment gas explosion-proof certification, surface temperature level, electrical protection level, to ensure that the equipment in the gas dispersion environment will not produce ignition sources, suitable for continuous process operations.

    Solvent and painting workshop

    The core risk of painting workshop is volatile solvent vapors, hazardous atmosphere more intermittent in the operating hours, mostly categorized as Zone 1, Zone 2 gas area.

    This type of scene focuses on safeguarding the explosion-proof performance of the electric control system, hand-held operators, and mobile equipment, to avoid sparks generated during the start-stop and operation of electrical components, and ignition of suspended vapors.

    Flour grain and oil processing workshop

    Grain and oil powder workshop is a typical dust explosion-proof scenarios, corresponding to 20, 21, 22 dust classification. The core risk is the dust suspension explosion cloud and dust accumulation on the surface of the equipment.

    Selection focuses on the dustproof sealing of the entire equipment, the upper limit of the surface temperature, electrostatic discharge structure, to avoid high-temperature surface ignition accumulation of dust, while eliminating the friction of mechanical sparks.

    Carbon black and coal powder plant

    Coal, carbon black powder density, accumulation speed, in addition to the risk of dust explosion, there are also high-intensity mechanical friction, electrostatic accumulation of potential hazards.

    The equipment needs to strengthen the mechanical explosion-proof design, optimize the material and structure of the friction parts such as wheels, brakes, transmission, etc., and at the same time, match with efficient electrostatic discharge device to adapt to high dust and high friction working conditions.

    Battery powder new material workshop

    New energy materials workshop is a mixed risk scenario, there are solvent vapor gas risk and ultra-fine powder dust risk, can not apply a single explosion-proof system.

    Selection needs to be combined with the characteristics of dual sources of danger, while meeting the gas and dust explosion-proof standards, optimized for temperature control, dust, anti-static, fire flowers multiple configurations.

    High-risk area maintenance lifting operations

    A lot of factory fixed process equipment without moving, but overhaul operations require temporary lifting equipment into the hazardous area. Selection of this type of scenario focuses on the scope and length of the approved equipment into the hazardous area.

    Short-term intermittent maintenance operations, can be adapted to the basic explosion-proof level of the corresponding zone; long-term fixed maintenance operations, in accordance with the normalization of the hazardous area standard selection.

    Procurement must verify the core technical parameters

    The compliance of explosion-proof equipment is reflected in the breakdown parameters. Checking each parameter at the procurement stage is a key step to avoid selection errors and ensure project compliance.

    Hazardous source type

    Clarify whether the site is a single gas, a single dust, or a gas-powder mixture of hazardous sources. Different media corresponding to the explosion-proof structure, certification standards, the focus of protection is completely different, is the basis of all selection parameters.

    Hazardous area level

    Strictly against the project survey report marked ATEX, IECEx area level, confirm the gas 0/1/2 zone or dust 20/21/22 zone division, all equipment protection level must match the corresponding regional standards.

    Equipment category attributes

    Distinguish between the types of procurement equipment, cranes, hoists, motors, electric control boxes, remote controls, lighting equipment, explosion-proof parameters are different, can not be uniformly applied to a set of standards.

    Surface temperature limits

    The maximum surface temperature during operation of the equipment is one of the core indicators of explosion-proof. It must be lower than the lowest ignition point of the combustible medium on site, to avoid direct ignition of gas or dust on the surface of the high temperature, which is a key parameter that many purchasing is easy to ignore.

    Core protection method

    Refuse to generalize the concept of “explosion-proof”, clear equipment specific protection principles, such as explosion-proof, increased safety, intrinsic safety, dust sealing protection. There are obvious differences in the hazardous scenarios and safety levels for different protection methods.

    Site environmental conditions

    Comprehensive consideration of the site humidity, corrosivity, dust accumulation, ventilation conditions, process residual media and other factors. High humidity, corrosive environments require additional strengthening of equipment sealing and anti-corrosion design to ensure long-term stability of explosion-proof performance.

    Equipment control mode

    According to the operating scenarios to choose the handle control, wireless remote control, cab control mode. Priority is given to remote control in high-risk confinement scenarios to reduce the risk of close contact between personnel, while supporting the corresponding explosion-proof level of control accessories.

    Mechanical risk point protection

    Focus on verifying the explosion-proof design of brakes, traveling wheels, transmission structures, and metal contact points to eliminate mechanical ignition sources such as friction sparks, impact sparks, and electrostatic buildup.

    Operation and maintenance adaptability

    Confirm that the explosion-proof structure of the equipment is convenient for daily inspection, parts replacement and troubleshooting. Protective structure can not sacrifice the convenience of operation and maintenance, otherwise the long-term use of inadequate operation and maintenance will lead to the failure of protection.

    Reliable explosion-proof equipment supplier screening criteria

    Explosion-proof equipment belongs to special industrial equipment, general equipment manufacturers do not have special R & D and production capacity. The industry experience and technical strength of the supplier directly determines the compliance and safety of the equipment.

    Verify the professional experience in high-risk working conditions

    Priority is given to manufacturers that are deeply engaged in the explosion-proof field and specialize in high-risk industrial scenarios. Different from ordinary industrial lifting equipment manufacturers, professional manufacturers are familiar with the risk of various types of gas, dust explosion-proof working conditions pain points, can accurately match the appropriate program.

    Verification of similar landing project cases

    Focus on checking the manufacturers in the oil and gas, chemical, powder, new energy, pharmaceutical and other high-risk industries real landing projects. A wealth of similar cases, on behalf of the manufacturer’s selection program and equipment quality verified by the real working conditions.

    Evaluation of professional engineering adaptability

    High-quality suppliers will not directly apply the general model offer, will take the initiative to check the site of the source of danger, the level of the region, the operating conditions, targeted recommendations to match the explosion-proof program, to avoid the waste of high matching or low matching unsafe.

    Verification of a full set of formal technical data

    Regular manufacturers can provide equipment assembly drawings, electrical schematic diagrams, explosion-proof protection, accessories, operating manuals, test reports and other complete sets of information to fully meet the acceptance of all types of projects around the world for the record.

    Confirmation of explosion-proof certification coverage

    Focus on checking the explosion-proof certificate to match the equipment model, applicable regional standards, local compliance system. Ensure that the certificate is real and effective, and fully match the procurement of equipment and project location specifications, to avoid problems such as certificate arbitration, scope inconsistency and so on.

    Verification of core parts compliance

    Explosion-proof motors, brakes, limit switches, electronic control boxes, remote controls, sensors and other core accessories, must all have the corresponding explosion-proof qualifications, not only the host explosion-proof, ordinary configuration of accessories.

    Clear testing, installation and commissioning services

    Confirm in advance the scope of services provided by the manufacturer, including factory explosion-proof performance testing, on-site installation guidance, machine commissioning, personnel training, etc., to ensure that the equipment can be put into operation in a compliant manner after entering the field.

    Verification of after-sales and spare parts security capabilities

    The operation and maintenance of high-risk explosion-proof equipment requires very high standardization, manufacturers need to have a long-term after-sales response, supply of original spare parts, operation and maintenance guidance to ensure that the equipment to maintain long-term explosion-proof performance.

    explosion-proof crane for different scenarios

    Procurement selection of common misconceptions

    Most of the problems of explosion-proof selection, are derived from the cognitive bias in the procurement stage, seemingly reasonable choice, will give the plant long-term safety and production of buried hidden dangers.

    The explosion-proof level as a unified standard, mistakenly believe that all explosion-proof equipment can be common, ignoring the essential difference between gas and dust explosion-proof system.

    Confusing gas hazardous area and dust hazardous area selection logic, gas explosion-proof equipment instead of dust explosion-proof equipment, protection is completely substandard.

    The pursuit of the highest level of explosion-proof, not combined with the actual working conditions, resulting in a substantial waste of equipment procurement costs.

    Only focus on the explosion-proof marking, ignoring the equipment surface temperature limits, high temperature surface there is still a risk of ignition medium.

    Default all high-risk areas of the plant need the same type of equipment, ignoring the risk level differences between different operating areas.

    Do not check the explosion-proof certificates to adapt to the region, resulting in equipment certificates do not meet the project’s local standards, can not pass the acceptance.

    Only verify the explosion-proof qualification of the host, ignoring the compliance of the motor, electronic control and other core accessories, there are loopholes in the overall protection.

    Procurement stage did not plan for the later maintenance and operation and maintenance programs, equipment for long-term use after the gradual failure of explosion-proof performance.

    Frequently Asked Questions

    What is the core meaning of explosion-proof grade?

    Explosion-proof rating is a standard for measuring the safe operation of equipment in high-risk explosive environments, which specifies the protection methods, applicable hazardous areas, temperature limits, and ignition source prevention and control capabilities of the equipment. The core role is to define the high-risk scenarios to which the equipment is adapted, and to guarantee that the equipment will not become a source of ignition for explosions in flammable and explosive environments.

    Is the selection for gas and dust hazardous areas the same?

    Not at all. The gas scenario adopts the 0/1/2 district grading standard, focusing on electrical spark prevention and control; the dust scenario adopts the 20/21/22 district grading, focusing on dustproof sealing, temperature control and static electricity prevention and control. The two systems are completely independent of each other in terms of certification, structural design and protection logic, and cannot be mixed.

    Does the project have to use the highest level of explosion protection?

    No, it does not. The highest level of explosion-proof equipment is only suitable for continuous high-risk core process areas. Ordinary intermittent hazardous scenarios, the use of the basic level of compliance to match the working conditions can be blindly high with only increased procurement and operation and maintenance costs, will not enhance the safety factor.

    How to determine whether the lifting equipment enters the hazardous area?

    The main body of the equipment, its running track, and the scope of operation are subject to whether it covers the labeled hazardous area or not. As long as any part of the equipment operation process into the high-risk area, you must use the corresponding explosion-proof level of equipment, can not be based on the length of the operation as a criterion.

    In addition to the explosion-proof certificate, what else needs to be verified?

    Need to check the surface temperature parameters of the equipment, the design of the protective structure, the core components of the explosion-proof qualification, local compliance standards, a full set of technical drawings, factory test records, operation and maintenance specifications, etc., the certificate is only the basic conditions of access.

    Are the ATEX and IECEx systems identical?

    No. IECEx is the international general explosion-proof certification system, applicable to most countries in the world; ATEX is the exclusive explosion-proof directive of the European Union, applicable only to the EU regional projects. There are slight differences between the two certification processes, marking specifications, acceptance requirements, according to the local choice of the project.

    What project information do I need to provide to the manufacturer before requesting a quotation?

    You need to provide the type of industry, flammable and explosive media properties, hazardous area rating, equipment use, the country where the project is located, the site working drawings, temperature and humidity and environmental conditions, so that manufacturers can accurately match the explosion-proof program and compliance qualifications.

    explosion-proof crane for different scenarios

    Summarize

    High-quality explosion-proof lifting equipment manufacturers can not only provide compliant explosion-proof equipment, but also rely on a wealth of global experience in high-risk projects to provide customers with working conditions assessment, program selection, qualification docking, on-site commissioning, long-lasting operation and maintenance of the whole process services.

    Henan Mine Crane has been deeply engaged in the field of industrial explosion-proof lifting equipment for many years, adapting to ATEX, IECEx, NEC and other global mainstream explosion-proof standards, and can be customized for oil and gas, chemical industry, powder, new energy, pharmaceuticals and other types of high-risk scenarios, exclusive explosion-proof equipment solutions.

    If you are not sure of the explosion-proof level of the project, you can provide the industry medium, hazardous area level, equipment requirements and project drawings, our engineering team will provide you with accurate selection, issued by the explosion-proof compliance program.

    Henan Mine CraneDiscuss your requirements ↗
  • Everything You Need to Know About Gantry Cranes

    Everything You Need to Know About Gantry Cranes

    Everything You Need to Know About Gantry Cranes

    In the field of modern material handling, gantry cranes are indispensable core equipment, choose the right matching gantry cranes can make industrial production, logistics loading and unloading efficiency doubled, and choose the wrong equipment will not only result in the acquisition of equipment, site remodeling of the high cost of waste, but also buried in the operation process of the safety hazards, and become a major risk point in the production operation. This article will be a one-stop answer to all your questions about gantry cranes, to help you accurately match the production needs of the equipment program.

    What Is a Gantry Crane?

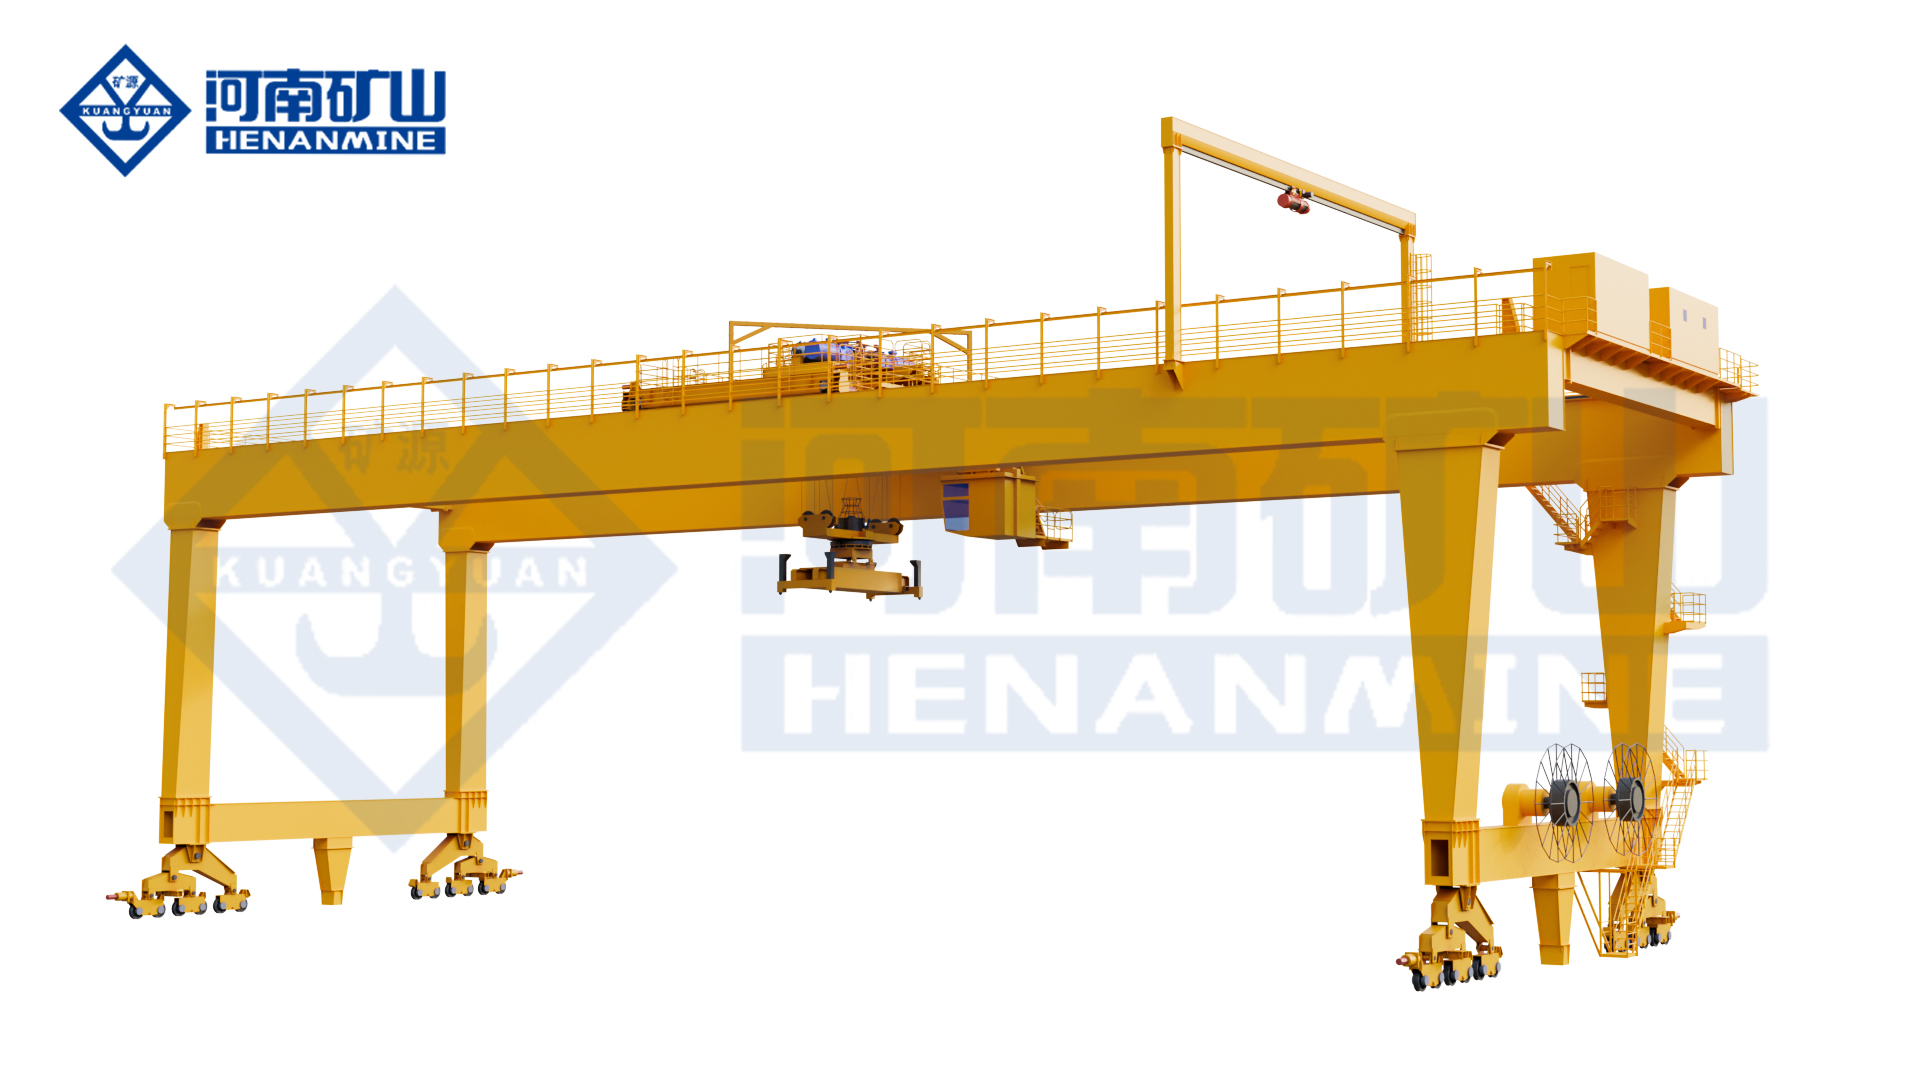
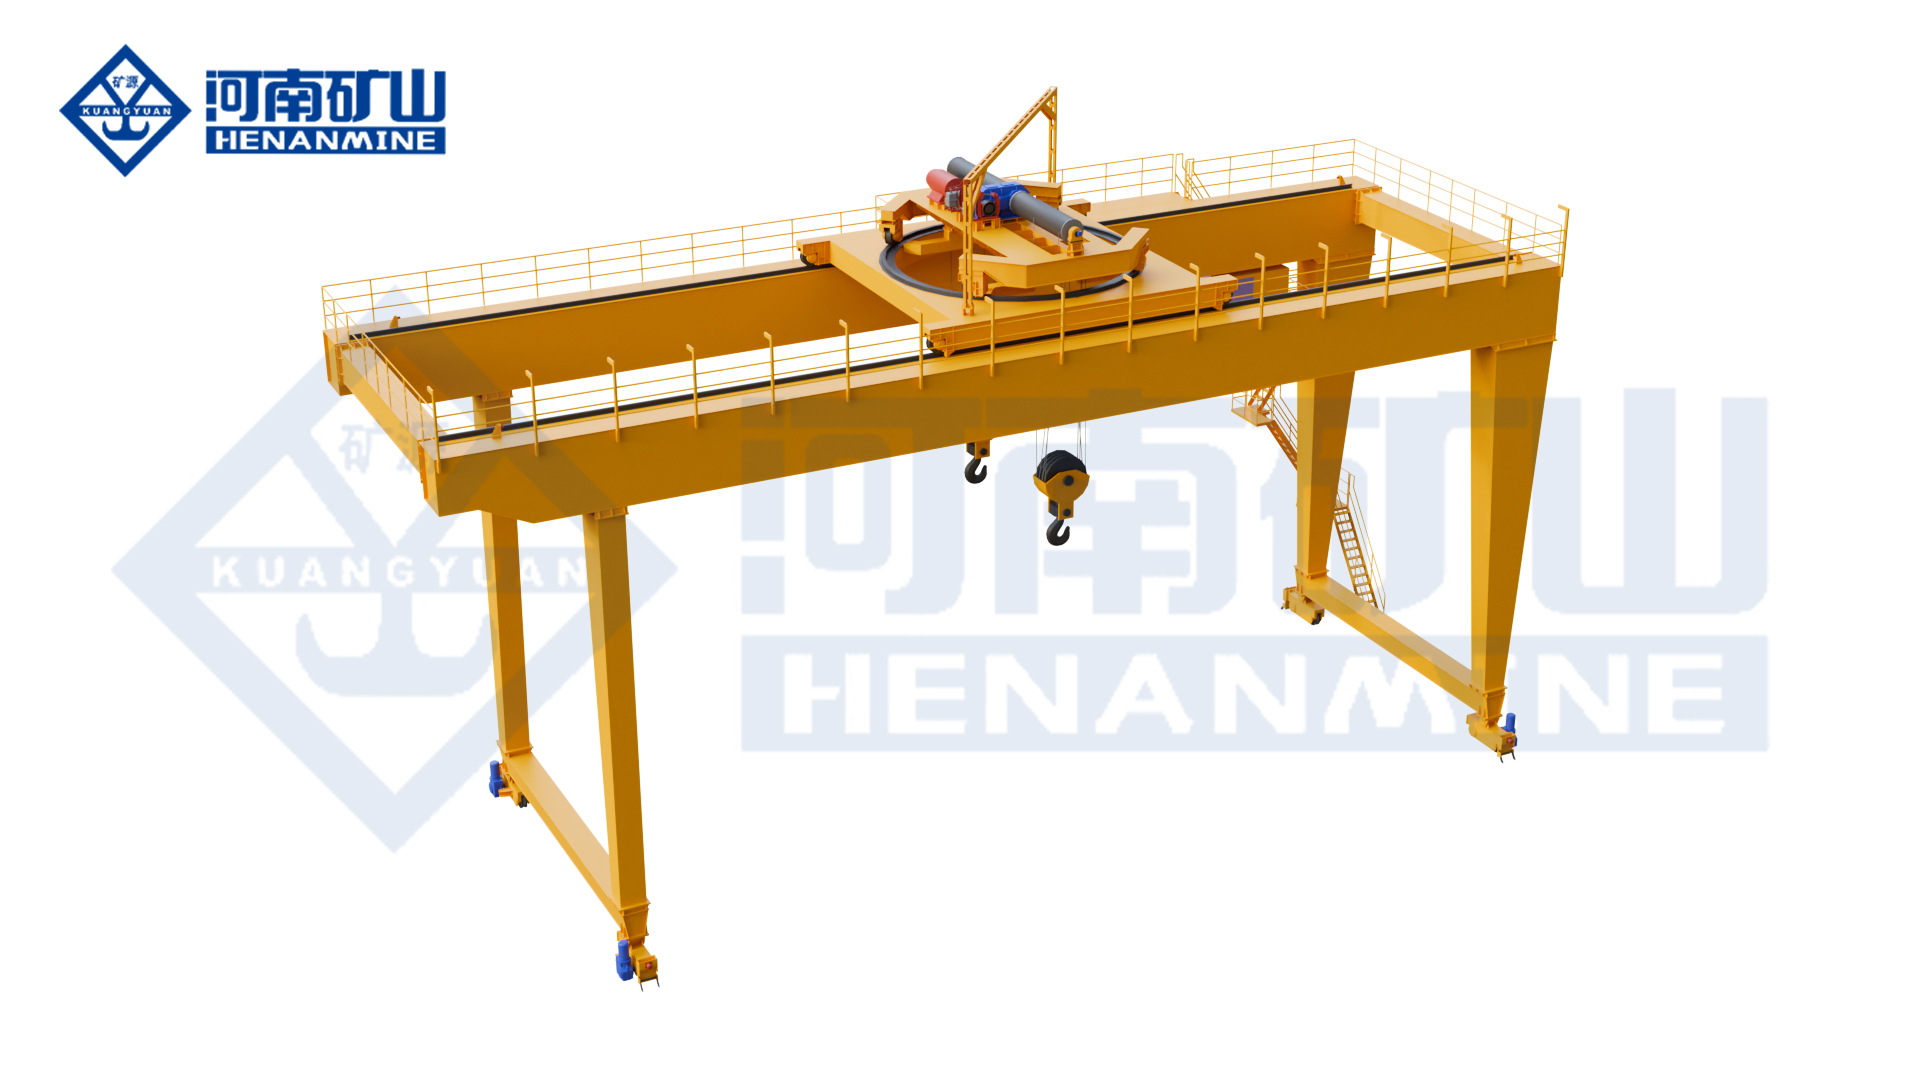
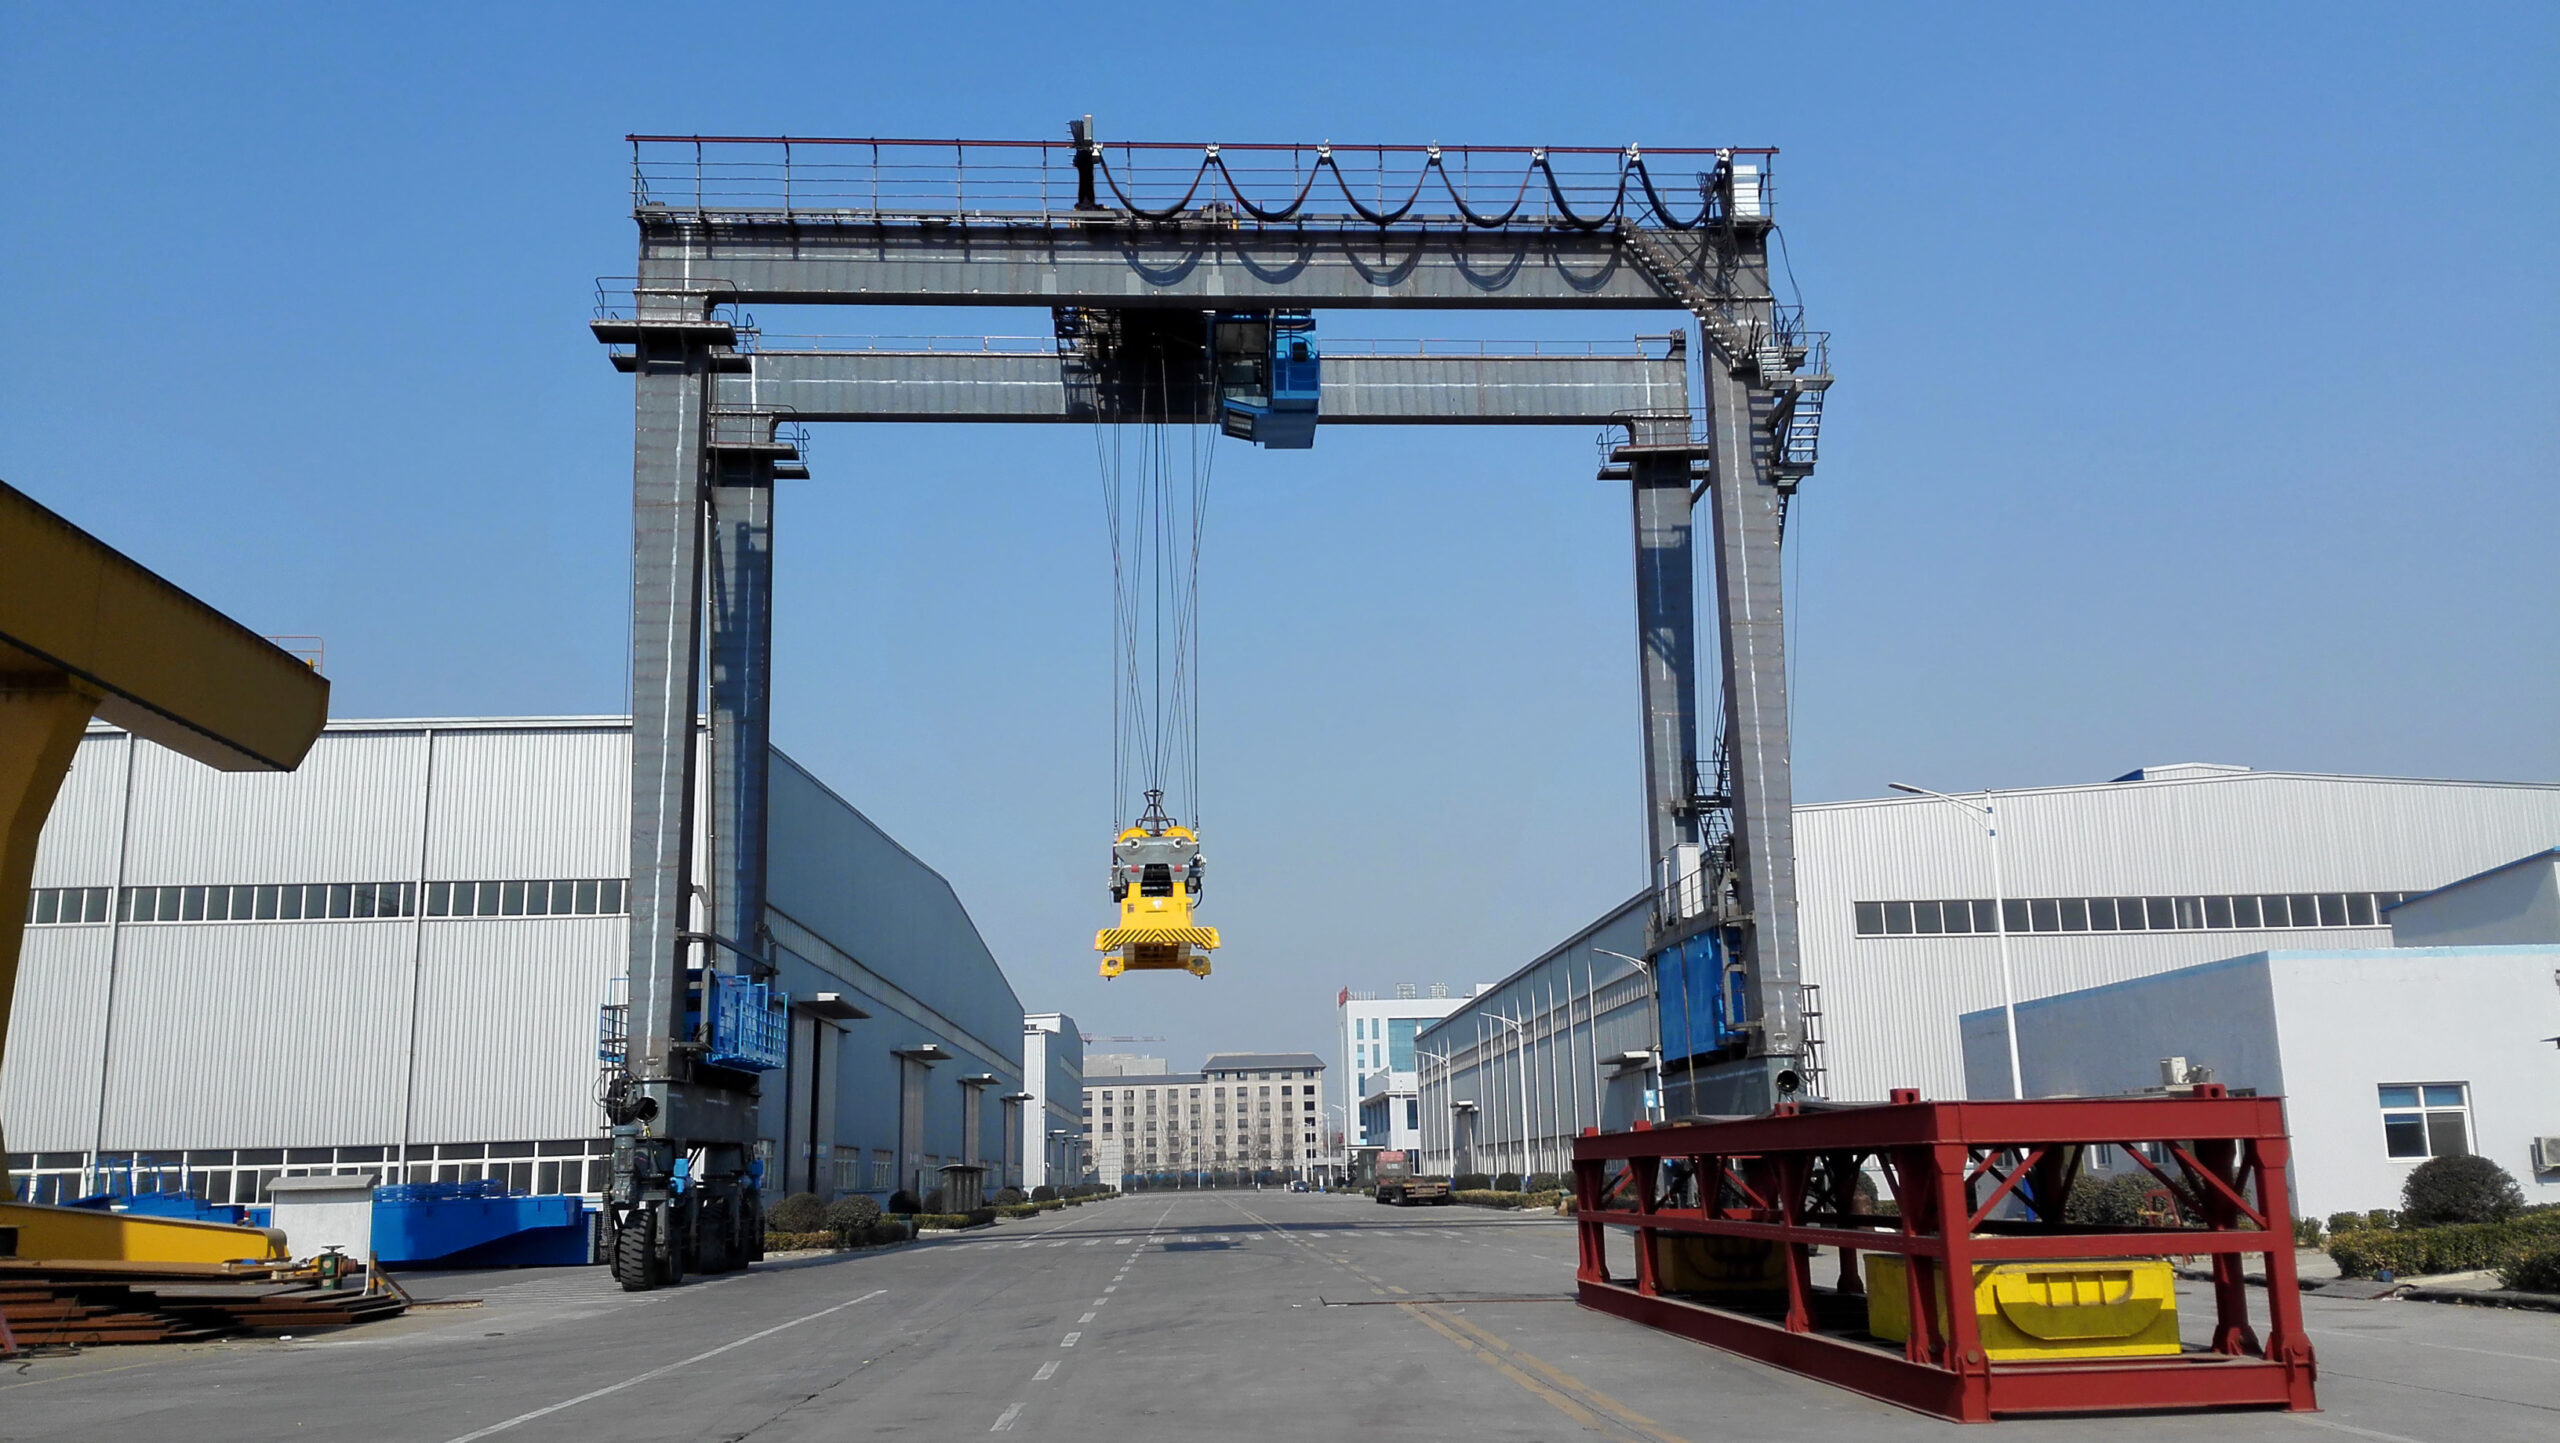
    Gantry Crane is an independent lifting equipment that does not need to rely on the building support, the outriggers carry the main girder and the lifting and running mechanism, which is widely used in industrial material handling. The core difference between it and overhead cranes is that it does not need to rely on the plant structure to support the weight, and it can run freely on the ground track or level ground, which makes it more flexible in adapting to the scenarios.

    From the basic structure point of view, the gantry crane is mainly composed of four core parts, each part works together to realize the accurate lifting and handling of materials:

    1. Main beam: Ss the load-bearing core of the equipment, it bears the main weight of the lifting load and is the skeleton structure of the gantry crane.
    2. Outriggers (with wheels/rails): Support the main beam and contact with the ground, the outriggers with wheels can realize the movement of the whole machine along the ground track, which is the walking part of the equipment and can drive the whole machine to move flexibly.
    3. Lifting trolley and hoist: Installed on the main beam, responsible for the vertical lifting and lowering of materials, is the core of the lifting function of the implementation of components.
    4. Control system: Including operation console, electrical wiring, sensors, etc., coordinates all the actions of the equipment to realize the precise control of lifting and moving.

    How Does a Gantry Crane Work?

    Gantry Crane’s operation process follows standardized steps, the institutions work together to achieve accurate handling of materials from lifting to the designated location, the entire operation process is clear and controllable, even for complex lifting operations, can be completed through standardized steps.

    1. Vertical lifting: Operate the lifting mechanism to lift the material vertically through the hook or spreader, leaving the ground to a safe height to avoid collision between the material and the ground obstacles.
    2. Horizontal movement: Manipulate the trolley system, drive the lifted material to move along the main beam in the horizontal direction, and adjust the material to the longitudinal direction directly above the whole machine. 3.
    3. longitudinal walking: Operate the machine to walk longitudinally along the ground track, carry the materials to the designated working position, and then slowly descend through the lifting mechanism to complete the precise placement of materials.

    heavy duty gantry cranes for industrial plants

    With the development of industrial automation, the degree of automation of the gantry crane is also increasing, the current mainstream automation configuration includes PLC programmable control, VFD variable frequency speed control, remote control operation, etc. PLC control can realize the automation of the workflow programming, reducing manual operation. VFD speed control makes the lifting and moving of the equipment smoother and avoids load shaking. Remote control allows the operator to complete the lifting operation in a safe area, enhancing operational safety.

    Types of Gantry Cranes

    Gantry cranes are available in a wide range of types, with different structural designs adapted to different load requirements, operating environments and production scenarios, ranging from light-duty material handling to ultra-heavy-duty industrial lifting, all of which have their own models.

    Single-girder gantry crane

    Single-girder gantry crane adopts the simple structural design of single main girder, the overall weight of the equipment is light, and the manufacturing process is simple, so the manufacturing cost and on-site installation cost are much lower than that of multi-girder model, which is the best choice for light duty operation scenarios. The rated lifting capacity is usually 1-20 tons, and the operation process is simple, so the daily inspection, maintenance and repair do not require complex professional tools, and the later operation and maintenance costs are also lower.

    Typical application scenarios: Material transfer in small and medium-sized workshops, loading and unloading of goods in warehouses, daily maintenance of factory equipment and parts handling.

    Best for: Focus on cost-effective equipment, lightweight material handling companies, or the basic lifting needs of start-up factories.

    Double-girder gantry crane

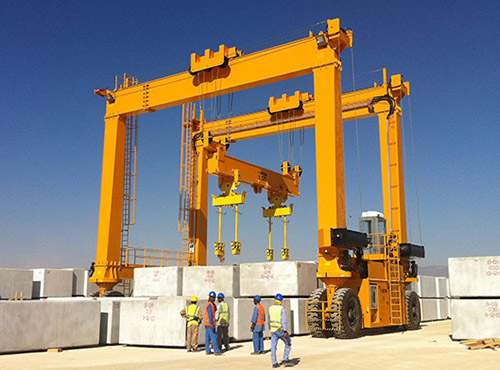
    Double-girder gantry cranes are equipped with two parallel main girders, compared with single-girder models, the structural strength and operational stability is greatly improved, and can withstand heavy loads and high-frequency continuous operation, and its rated lifting capacity can be up to 20-200 tons or more, and support for customized design according to the customer’s production needs, to meet the special lifting requirements.

    Double girder gantry cranes can be equipped with a variety of advanced configurations, such as double hoist lifting system, which can realize the balanced lifting of large volume materials. The lifting height can also be increased to meet the lifting requirements of high plants and large materials in the open air.

    Typical application scenarios: Billet and steel handling in steel mills, component lifting in precast concrete plants, and large equipment assembly in the heavy machinery manufacturing industry.

    Best for: Industrial enterprises with medium and heavy material handling needs and high operating frequency, pursuing the stability and durability of the equipment.

    Truss gantry crane

    The main beam and outriggers of truss gantry crane adopt lattice structure design, which greatly reduces the weight of the equipment itself compared with the solid web structure, and at the same time effectively reduces the wind resistance, which ensures the stability of the operation even in the outdoor strong wind environment, and is not easy to be affected by the wind and the equipment shaking. In addition, the steel consumption of truss structure is less, which can meet the lifting demand of large coverage while controlling the cost for large span operation.

    Typical application scenarios: Handling of reinforcement bars, formwork and prefabricated components in construction sites, loading and unloading of materials in open-air cargo yards, and lifting of bridge girders in road and bridge projects.

    Best for: Outdoor work is the main work, the work area is windy, the need for large-span lifting coverage of the engineering enterprises.

    Semi-gantry crane

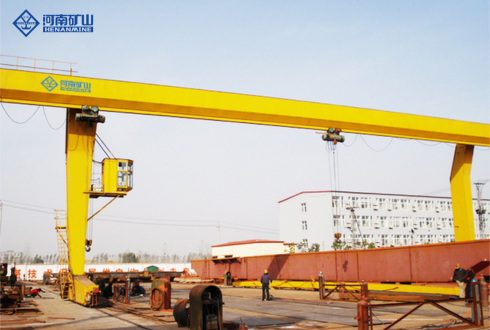
    Semi-gantry crane is a composite equipment that combines the advantages of gantry crane and overhead traveling crane, one side of the outrigger runs along the ground track, and the other side relies on the plant’s bull legs, columns and other architectural structures to build the track, without the need to set up a separate double-sided ground track, significantly saving the space occupied by the site, and also reduces the cost of site infrastructure.

    Semi-gantry cranes not only retain the flexible mobility of gantry cranes, but also use the building structure to realize the load-bearing, suitable for the site space is limited or part of the building structure can be used in the scene.

    Typical application scenarios: Material handling in workshops with existing traveling beams, cargo transfer in indoor and outdoor transition areas, and material transfer between workstations in production lines.

    Best for: Enterprises with limited space and existing building structures to utilize, or production scenarios that need to realize indoor and outdoor continuous material handling.

    Shipbuilding gantry crane

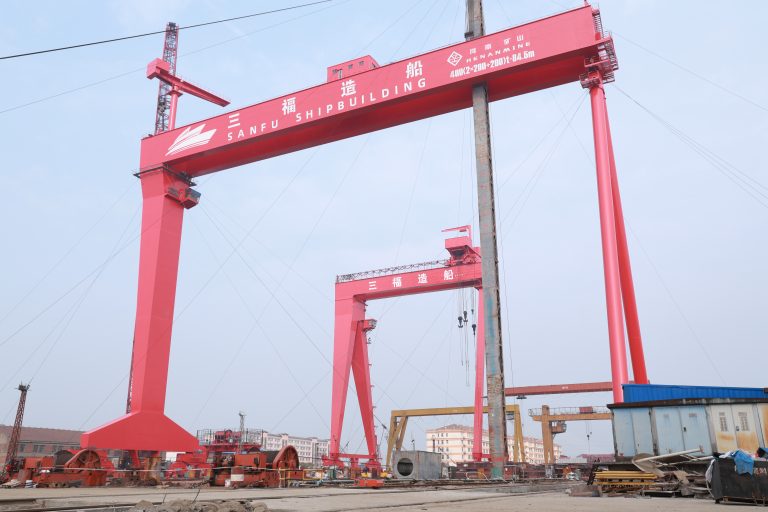
    Shipbuilding Gantry Crane, also known as Goliath Crane, is specially used for ultra-heavy, oversized material lifting equipment, its rated lifting capacity can easily reach 300 to 500 tons, and some customized models can even achieve 1,000-ton lifting, in the field of heavy equipment manufacturing is widely used and important role.

    Shipbuilding gantry cranes are equipped with a multi-hook synchronous lifting system, which can realize the balanced lifting of large-volume and shaped components, and at the same time, equipped with a high-precision control system, which can accurately control the lifting position to meet the needs of assembly of large structures.

    Typical application scenarios: Hull segment assembly and ship repair in shipbuilding factories, construction and installation of offshore platforms, and lifting of heavy steel components in large-scale steel structure plants.

    Best for: Shipbuilding, ocean engineering, heavy steel structure manufacturing and other enterprises that need super-heavy large lifting.

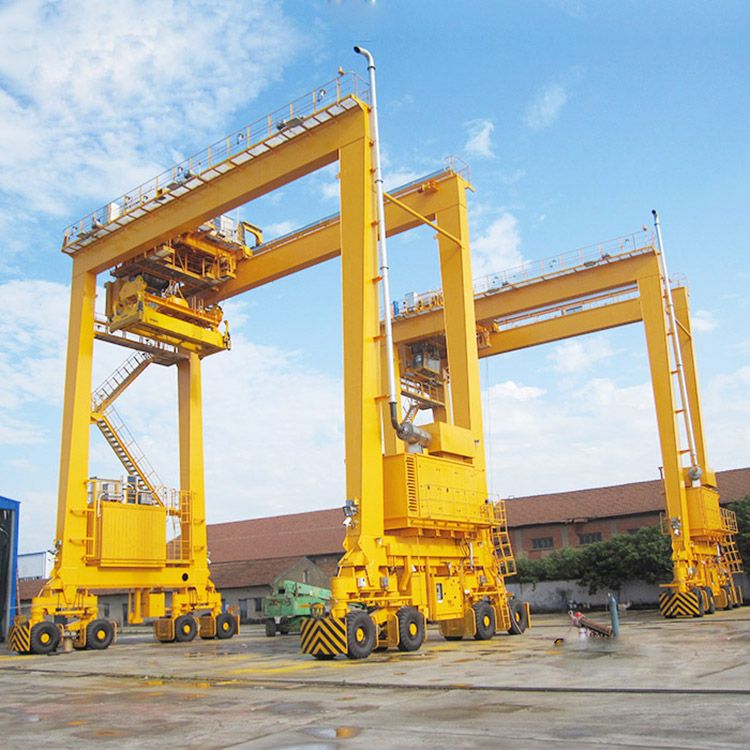
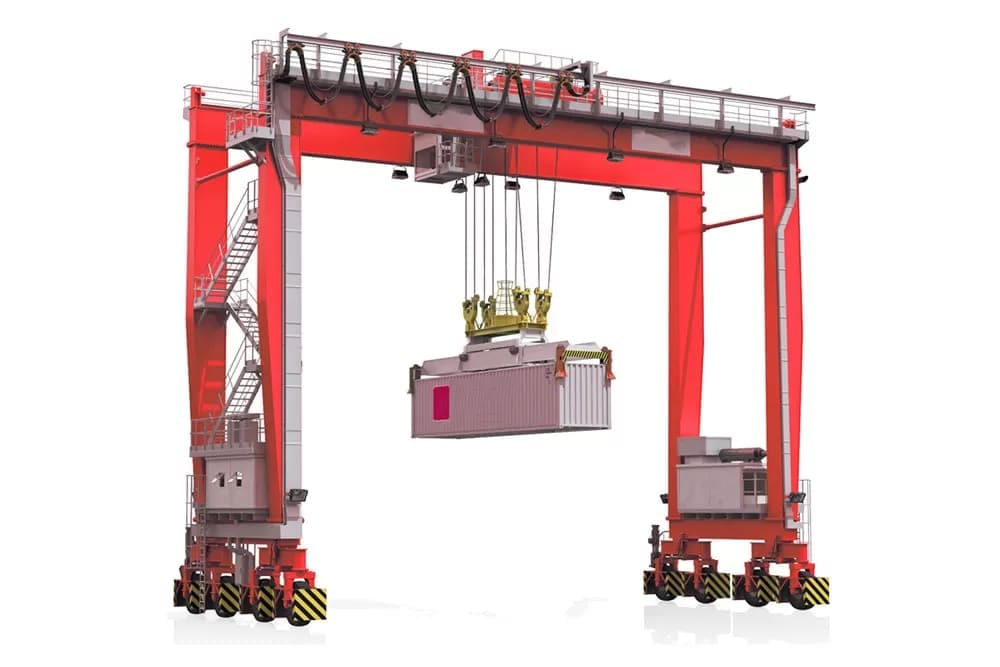
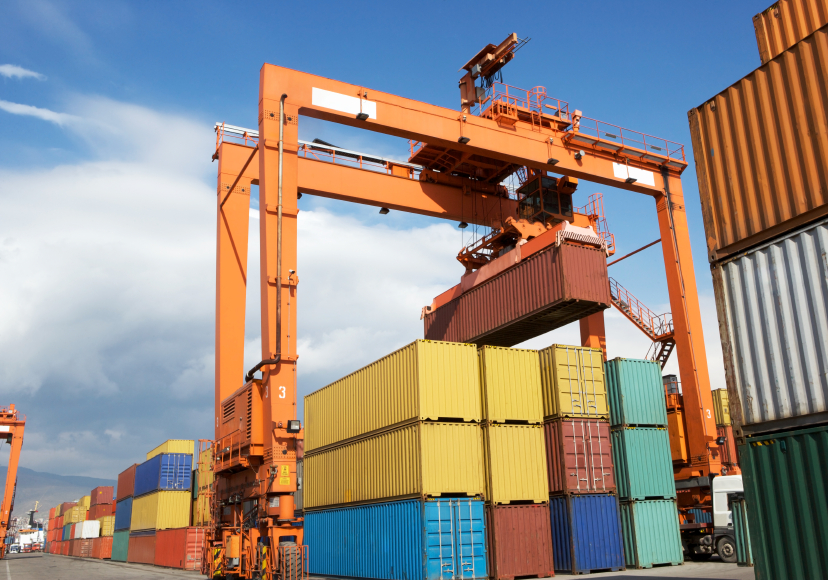
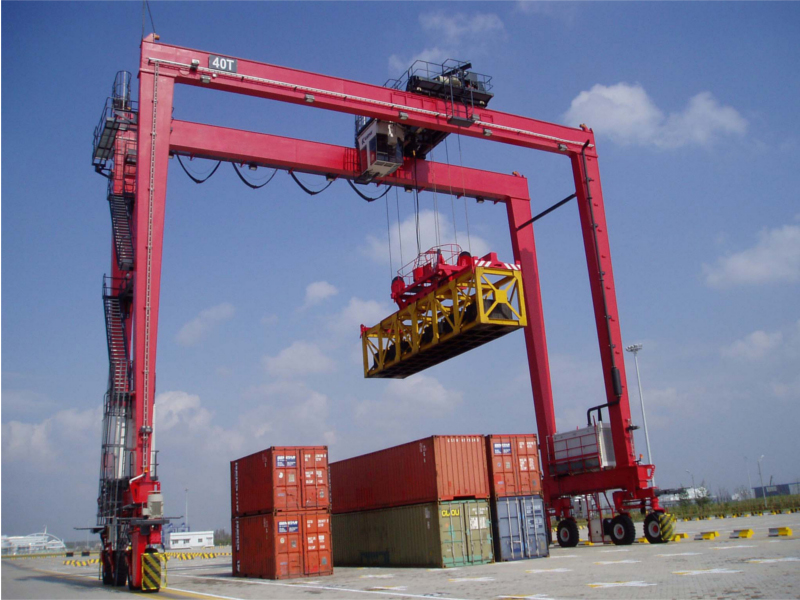
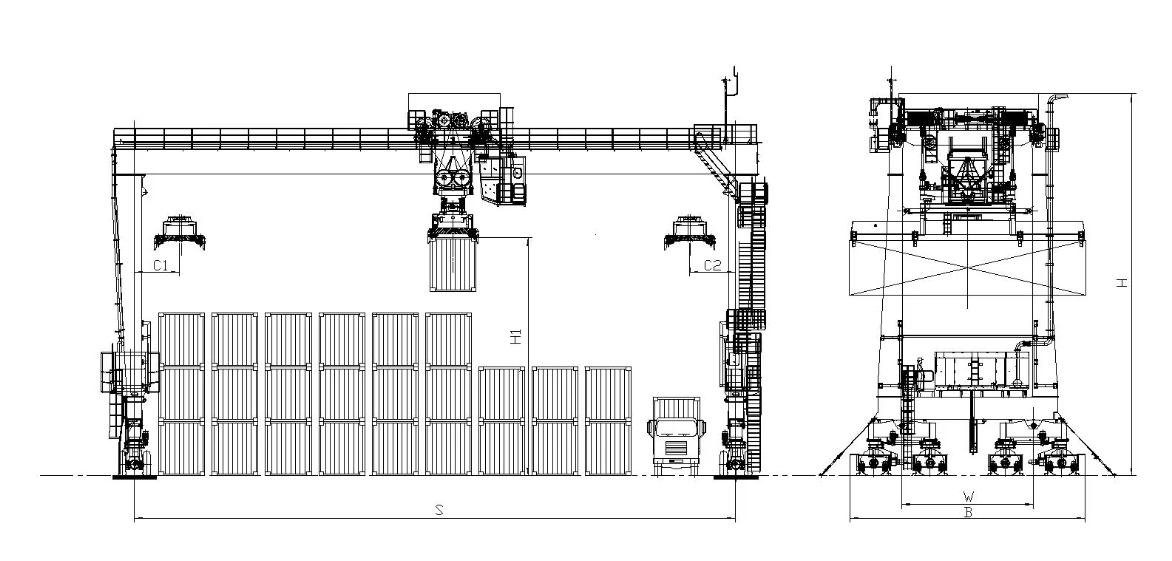
    Rail-mounted container gantry crane

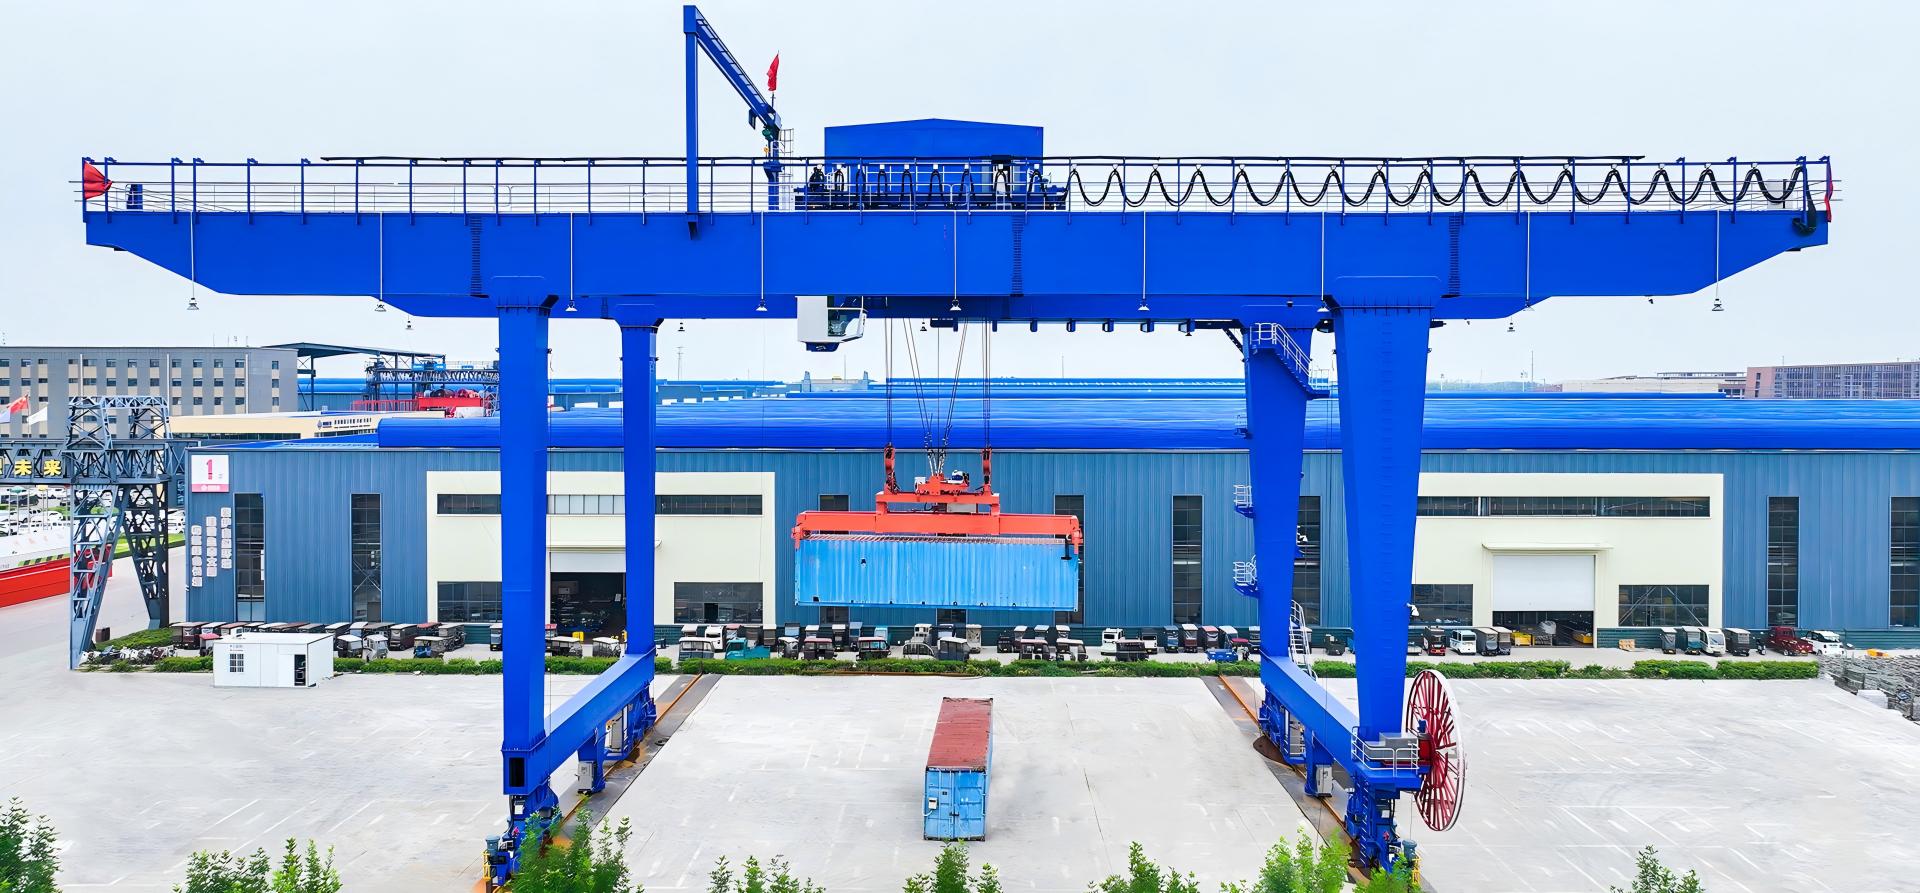
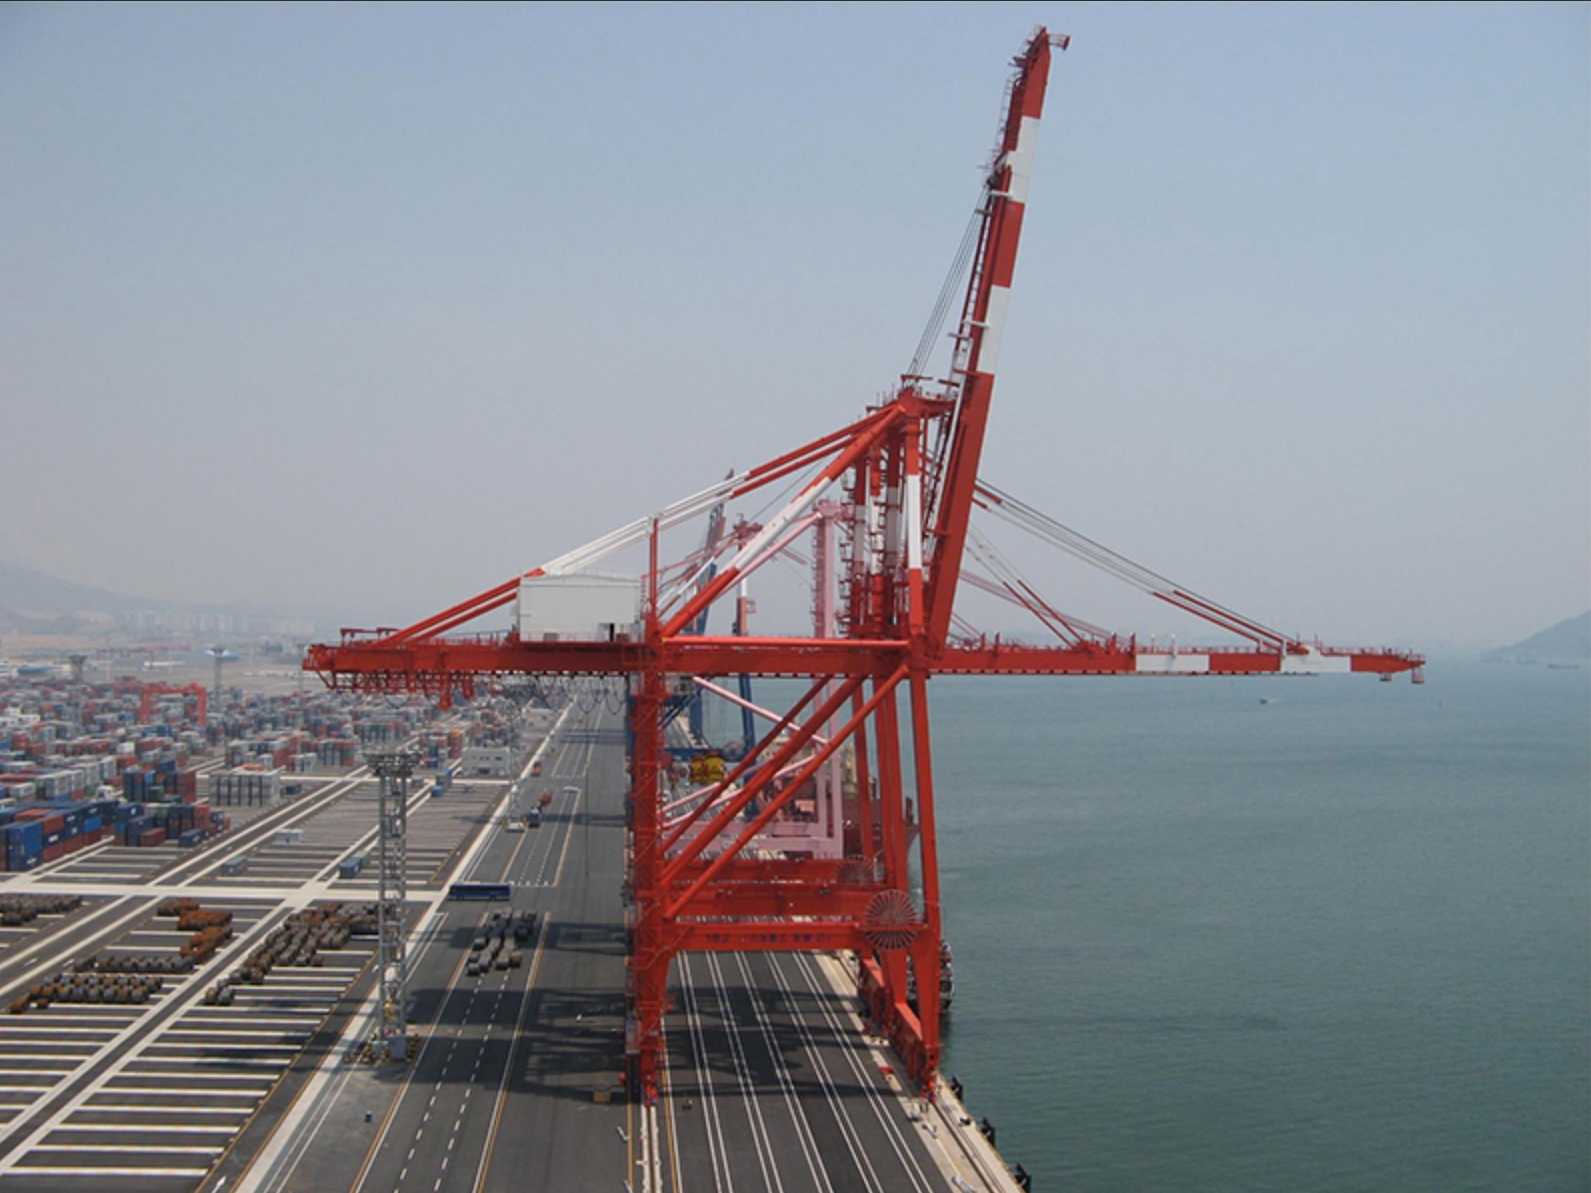
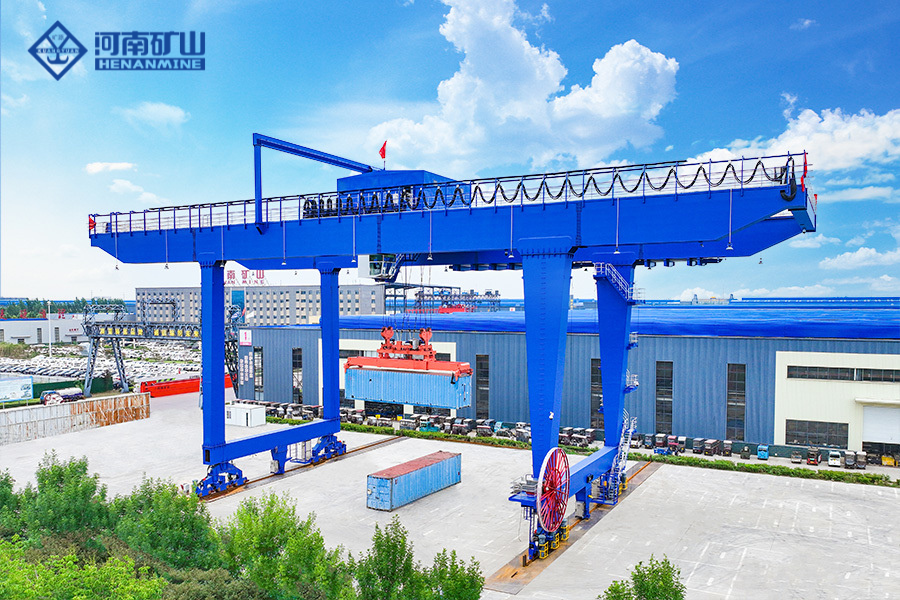
    Rail-mounted container gantry crane is specially designed for container handling, the whole machine runs along the fixed rail, the running accuracy and operational stability is very high, is the core loading and unloading equipment for container yard and logistics hub. This model supports fully automatic or semi-automatic control, which can realize precise stacking and fast loading and unloading of containers, significantly improve the efficiency of repetitive container operation and reduce the error of manual operation.

    Typical application scenarios: Container port yard operations, container loading and unloading at railroad freight stations, and container storage and transshipment in large logistics parks.

    Best for: Ports, freight stations and large logistics enterprises with large container throughput, pursuing efficient and standardized container handling.

    Get the Best Rail Mounted Gantry Crane Price

    Gantry Crane Applications

    Heavy duty gantry cranes for industrial plants have become the core equipment for material handling in various industrial fields due to their flexible structure, wide lifting capacity coverage and multi-scenario adaptability, which can be seen in everything from workshop assembly in the manufacturing industry to outdoor construction in the construction industry, and from loading and unloading of goods in the logistics industry to transshipment of containers in ports.

    Manufacturing and assembly

    Gantry cranes are mainly used in workshops for the handling of production equipment, lifting and loading of large molds, and assembly of heavy parts, such as lifting and loading of body frames in automobile manufacturing and handling of machine tools in machinery manufacturing, which can greatly enhance the efficiency of material flow in workshop production, and reduce the cost and risk of manual handling.

    Construction sites

    Gantry cranes are the core lifting equipment for construction sites, mainly used for steel, rebar, building formwork handling, prefabricated concrete panels, bridge girders lifting, as well as the dismantling of large-scale construction machinery on the construction site, suitable for construction sites in the open air, wide range of operation to meet the needs of various types of materials lifting during the construction process.

    Warehousing and logistics

    Gantry cranes are also suitable for loading and unloading of goods and storage in warehouses and logistics parks, such as loading and unloading of bulky goods on and off shelves, loading and unloading of trucks. Compared with forklift trucks and other equipment, they can realize material handling of greater weight and higher height, enhance the operational efficiency of warehousing and logistics, and meet the demand for efficient flow of modern logistics.

    Ports and shipyards

    In the field of ports and shipyards, gantry cranes are mainly used for loading and unloading of containers and bulk cargoes, as well as yard transfer. In the field of shipyards, gantry cranes are used for the assembly of hull segments, lifting and loading of ship parts and ship repair and maintenance, especially the ultra-heavy shipbuilding gantry cranes, which are the core production equipment of large shipyards, determining the shipyard’s ability to build large-scale ships.

    Maintenance and repair

    Gantry cranes are suitable for daily maintenance of factory equipment, lifting of large engines, maintenance of power facilities and other scenarios, such as turbine maintenance in power plants, steel rolling equipment maintenance in steel mills, and can flexibly enter the work area, complete the dismantling and loading of heavy equipment parts, providing convenient lifting support for equipment maintenance.

    Industry insight

    Core Advantages of Gantry Cranes

    Compared with other lifting equipment, gantry cranes can become the mainstream choice of modern material handling, the core stems from its structure and performance of multiple advantages, suitable for different industries, different scenes of lifting needs, the specific advantages are as follows:

    • No need to rely on building structures: Independent load-bearing design, without the use of plant bull legs, columns and other building structures, can be built and used in any site, the scene is very strong adaptability.
    • Indoor and outdoor work: Gantry cranes can be used as fixed lifting equipment in the workshop, but also in the outdoor open space, construction sites, harbors and other areas of operation, to achieve indoor and outdoor continuous material handling.
    • Flexible and movable: Gantry cranes can run freely along the ground track, with a wide range of operational coverage, and some light models can be quickly disassembled and assembled along the track, to adapt to temporary operational scenarios.
    • Lower installation costs: Gantry cranes do not require complex structural transformation of the building, only need to level the site and build a simple track, you can complete the installation, compared with overhead cranes, site infrastructure and equipment installation costs are significantly reduced.
    • Wide range of lifting capacity: From 1 ton light-duty models to super-heavy-duty models of more than 500 tons, the whole series of gantry cranes can meet all the needs from light-duty material handling to super-heavy-duty lifting of large parts, one-stop adaptation to the production needs of different enterprises.

    outdoor gantry cranes for construction sites

    Gantry Crane Load Capacity And Duty Classification

    One of the core indicators for the selection of gantry cranes is the equipment’s lifting capacity and duty class, which directly determines whether the equipment is suitable for the production and operation needs of the enterprise. Different lifting capacities and duty classes correspond to different operation frequencies and load requirements, which are divided as follows:

    Capacity range

    According to the different rated lifting capacity, gantry cranes can be divided into three categories, which are suitable for different load requirements.

    1. Light:Rated lifting capacity of 1-5 tons, suitable for light material handling, low frequency of operation, such as small warehouses for loading and unloading of goods.
    2. Medium:Rated lifting capacity 10-20 tons, suitable for medium load material handling, medium frequency of operation, such as small and medium-sized workshop equipment assembly.
    3. Heavy duty: Rated lifting capacity 50 tons and above, suitable for heavy load material handling, high frequency of operation, such as heavy lifting in steel mills and shipyards.

    Duty classes (A/B/C/D/E/F)

    The duty classes of gantry cranes are classified according to the frequency of operation and load status, from A to F, the intensity of work is gradually increased, which is the core index to judge the ability of continuous operation of the equipment.

    Class A/B: light duty working class, applicable to occasional operation scenarios, such as temporary lifting for equipment maintenance.

    Class C/D: Medium duty, suitable for medium frequency operation, such as daily material handling in warehouses.

    Class E/F: Heavy duty, suitable for high frequency, continuous operation, such as steel mills, ports, 24-hour continuous production.

    How to Choose the Right Gantry Crane

    The key to choose the right gantry crane is to combine their own production needs, site conditions and operating environment, comprehensive consideration of various factors, to avoid cost waste and safety hazards due to selection errors, the following is a professional procurement and selection recommendations, including the core factors for consideration and common avoidance of pitfalls:

    Key factors

    1. lifting capacity demand: According to the maximum weight of the daily handling of materials, to determine the rated lifting capacity of the equipment, it is recommended to reserve 10% -20% of the load margin, to avoid overloading operations.
    2. Span and lifting height: Span is determined according to the width of the working area, lifting height is determined according to the stacking height of the materials, lifting height, both of which directly determine the operating range of the equipment.
    3. Operating environment: Distinguish between indoor and outdoor operation; for outdoor operation, choose the truss model with good wind resistance; for corrosive environment, such as chemical plant area, choose the equipment with anticorrosive treatment.
    4. Mobility requirements: According to the size of the working area, determine whether the equipment needs to be moved frequently, such as the need for temporary work, you can choose the track easy to dismantle the light models.
    5. Working level: according to the frequency of operation, continuous 24-hour operation needs to choose E / F class heavy-duty working level, daily low-frequency operation can choose A / C class.

    Customized Solutions

    Tell us your specific lifting capacity, operating span, lifting height, operating environment and production needs, Henan Kuangshan will customize your exclusive gantry crane solutions, from equipment selection, site planning to installation and commissioning, one-stop service, so that your lifting equipment accurately match the production needs.

    Tips for Effective Gantry Crane Maintenance

    Safe operation and regular maintenance of the gantry crane is to ensure the normal operation of the equipment, to extend the service life, to avoid safety accidents at the core, the daily operation of the need to strictly follow the safety norms, and at the same time to establish a perfect maintenance system, the specific safety points and maintenance list is as follows:

    Daily inspection

    Every day before the operation, need to carry out a comprehensive safety inspection of the equipment, to confirm that there is no fault before starting the operation, focusing on the following parts of the inspection:

    1. Wire rope and hook: Check whether the wire rope has broken wire, wear and tear, loose strand phenomenon, whether the hook has deformation, cracks, and whether the safety catch is intact. 2. control system: check the operator’s console, and make sure that there is no malfunction before starting the operation.
    2. Control system: Check whether the operating table button, remote control is sensitive, limit switch, emergency stop button can work properly.
    3. Walking and lifting mechanism: Check the fit of wheels and tracks, whether the lifting trolley is running smoothly, and whether there is any abnormal noise.
    4. Electrical wiring: Check whether the wires and cables are damaged or aging, and whether the wiring is firm and without leakage.

    Preventive maintenance

    Regular professional maintenance of the equipment, timely replacement of wearing parts, lubrication of key parts, to avoid failure due to aging parts, the core maintenance content:

    1. lubrication maintenance: Regularly add lubricant to the rotating parts such as wheel bearings, trolley pulleys, and gears of the lifting mechanism to ensure flexible rotation. 2. structural inspection: Monthly inspection of the main machine, and monthly inspection of the main machine.
    2. Structural inspection: Monthly inspection of the main beam, legs and other steel structures to see whether there are deformation, cracking, welding points off and other problems, and timely reinforcement and repair.
    3. Replacement of wearing parts: according to the frequency of use, regularly replace the wire rope, brake pads, pulleys and other wearing parts to avoid safety accidents caused by wear and tear of parts.
    4. Electrical maintenance: inspect and debug electrical parts such as motors, inverters, sensors, etc. every quarter to ensure the stable operation of the electrical system.

    Safety systems

    Qualified gantry cranes are equipped with perfect safety protection system, the operation needs to ensure that all the safety systems work properly, can not be arbitrarily disassembled or closed, the core safety systems include:

    1. Overload protection system: When the load exceeds the rated lifting capacity of the equipment, it will automatically cut off the lifting power to prevent overloading.
    2. Limit protection system: Including lifting height limit, trolley travel limit, the whole machine travel limit, to prevent the equipment from over-traveling operation caused by collision.
    3. Emergency stop system: All parts of the equipment are equipped with emergency stop buttons, which can quickly cut off the power supply of the equipment and stop all actions in case of emergency.
    4. Anti-shaking system: Some medium and high-end models are equipped with load anti-shaking system, which reduces the shaking of the material during lifting and moving and improves the stability of lifting.

    Conclusion

    In modern industry and logistics system, gantry crane is not only the basic handling equipment, but also the key equipment that affects the production efficiency and operational safety. Through in-depth understanding of its structural principles, type differences and application scenarios, enterprises can realize more efficient and stable material flow under different working conditions, while effectively avoiding the cost waste and potential risks caused by improper selection.

    From equipment selection to daily use and maintenance management, every aspect of the gantry crane is directly related to the operational performance of the enterprise. Combined with the actual load demand, operating frequency and site conditions, reasonable matching models and establish a standardized maintenance system, not only to extend the service life of the equipment, but also to continue to protect the operational safety and productivity, to achieve long-term stable operation.

    Henan Mine CraneDiscuss your requirements ↗
  • Electromagnetic Crane vs. Grab Crane: Which Fits Steel Mills Better?

    Electromagnetic Crane vs. Grab Crane: Which Fits Steel Mills Better?

    Electromagnetic Crane vs. Grab Crane: Which Fits Steel Mills Better?

    Industry mills transport large quantities of metal during every shift, and the crane attachment used for each task will influence throughput, cost, and safety. The two main types of container used in the industry are the electromagnetic crane, which has a powered magnet for lifting, and the grab crane, which has a mechanical or hydraulic device to operate a clamshell.

    Each has its advantages, and choosing the best system depends on the kind of material you are moving and where you are moving it. This article describes the pros and cons of each type,  how to decide which is best for which bay, and what the pros and cons of each system are.

    What Is an Electromagnetic Crane?

    An electromagnetic crane is similar to an overhead or gantry crane but uses a circular electromagnet in the place of a hook or bucket. When the electromagnet is energized,  the force when the magnetic fields when energized is intense enough to grip the steel directly and move the load without the need for slings, chains or rigging.

    Electromagnetic cranes are used in all steel mills, scrapyards, shipbuilding and auto plants, and especially where coils, plates or fairly clean ferrous scrap are passing from one operation to another very rapidly.  Almost all large industrial units have a battery-backed, power-off holding system so that the magnet maintains its hold when the power is shut off – an essential safety feature where the lifting operation is taking place above people.

    What Is a Grab Crane?

    A grab crane is actually an overhead or gantry crane with a clamshell grab suspended underneath it instead of a magnet or a hook. The jaws of the grab open and close (normally by a hydraulic cylinder) to physically clamp around the general or irregular shape.

    Since the grab crane does not magnetize and clamp, it has the advantage of being able to empty non-magnetic materials like iron ore, coke, limestone, slag, non-ferrous metals, mixed and bundled scrap.  Therefore, it is the standard piece of equipment in the raw material yard and any bay where loads cannot be expected to be purely clean, magnetic steel.

    Electromagnetic Crane vs. Grab Crane: Key Differences at a Glance

    Factor Electromagnetic Crane Grab Crane
    Material compatibility Ferrous materials only (steel, iron) Ferrous and non-ferrous, mixed and irregular materials
    Typical cycle speed Roughly 30–40% faster on compatible ferrous loads Slower, but consistent across material types
    Weather resilience Best suited to controlled, indoor environments Handles rain, snow, dust, and temperature extremes reliably
    Automation level High — no manual rigging or slinging needed Moderate — hydraulic grabs are automated, but the load itself is more variable
    Versatility Limited to whichever magnet is configured for the load High — one grab can handle diverse material streams
    Power draw / operating cost Higher continuous power consumption Primarily hydraulic; different cost profile
    Component wear Fewer, more expensive electrical component replacements More frequent, lower-cost mechanical component replacements
    Typical service life 20–30 years with proper maintenance 20–30 years with proper maintenance
    Best-fit zones Coil/finishing bays, billet handling, clean ferrous scrap Raw materials yard, mixed scrap yard, outdoor stockpiles

    Where Electromagnetic Cranes Win in a Steel Mill

    Coil, plate, and billet handling

    The magnetic lifting tool can be used to lift the coil, which can save the tedious and low-speed procedure of manually aligning the C hook with the inner hole of the coil.Magnetic adsorption and unloading release can be completed instantaneously, which is also the core reason why electromagnetic cranes and special coil cranes are widely used in rolling workshops and finishing span areas.

    Hot billet transfer

    The temperature of billet produced by continuous casting process can reach 800 DEG C or more.Magnetic lifting tools do not have the structure of physically clamping workpieces, which can greatly reduce the probability of collision damage on the surface of high temperature steel that is still in the forming stage. Compared with mechanical grab, it has very prominent advantages in this working condition.

    High-volume, single-material operations

    For enterprises with daily iron-containing material volume of more than 50 tons, including steel coil processing manufacturers, steel plate processing manufacturers, steel distribution centers, etc., the electromagnetic lifting system can reap considerable economic benefits.The operation time saved by a single lifting will continue to accumulate in the frequent lifting day after day, and the overall operation efficiency will be significantly improved.

    Foundry and scrap-return handling

    Cast iron ingot, steel ball, pig iron block and clean machining steel scrap and other materials, are suitable for magnetic lifting operations.With good adaptability and operation advantages, electromagnetic crane has become the standard lifting equipment for foundry workshop and scrap recovery section.

    Where Grab Cranes Win in a Steel Mill

    Raw materials yards

    Iron ore, coke, raw coal, limestone and other burden raw materials need to be transported into the smelting furnace after storage, and these materials cannot be hoisted by magnetic equipment.Therefore, clamshell and hydraulic grab crane are the only practical equipment selection for raw material storage yard operation.

    Cold or coated billets

    After the billet is cooled or coated, the adsorption and clamping force of electromagnetic crane will be greatly attenuated, and the lifting stability will be greatly reduced.For cooled billets and coated billets stored at normal temperature and transferred in storage yard, mechanical clamp is the preferred scheme with higher safety and more stable operation.

    Mixed and non-ferrous scrap

    For scrap mixed with iron and nonferrous metals, bundled scrap and irregular scrap, mechanical grab operation adaptability is better.Mechanical grab relies on physical wrapping to clamp materials, which is different from magnetic adsorption principle, and can effectively solve the problem that mixed and irregular wastes cannot be hoisted stably.

    Outdoor and exposed installations

    Mechanical grab lifting system has excellent environmental adaptability, can withstand rain, snow, dust, high and low temperature and other complex outdoor conditions, stable performance is not easy to damage, waste dump, port, open yard and other unshielded operation area standard equipment.However, in such complex open-air environment, the operation performance and reliability of magnetic lifting equipment are difficult to be effectively guaranteed.

    Cost and Lifecycle Comparison

    There is no absolute cost advantage between the two types of lifting equipment. The overall cost of ownership mainly depends on the frequency of equipment operation and the type of materials handled. The cost differences are as follows:

    • Initial investment cost: grab crane early procurement investment is lower, equipment configuration flexibility is strong, can adapt to a variety of complex conditions quickly adjust the configuration scheme.
    • Operation cost: electromagnetic crane needs to be continuously energized to maintain magnetic lifting force, and the whole process continues to consume electricity; grab crane mainly relies on hydraulic system to complete the operation, and the energy consumption operation mode is significantly different from electromagnetic equipment.
    • Maintenance cost and mode: electromagnetic lifting system fault maintenance frequency is lower, but the single maintenance cost is higher, the core maintenance items are concentrated in the coil, power components replacement and other high-priced accessories.The grab lifting system has more mechanical loss parts, higher daily maintenance and repair frequency, but the single maintenance cost is low, and the overall maintenance threshold is lower.
    • Equipment service life: Under the premise of standardized maintenance, the service life of two types of equipment can reach 20 to 30 years.Therefore, the core consideration for equipment selection is not basic durability, but the long-term benefits brought by labor cost savings and improved work cycle efficiency.
    • Productivity return benefit: For large-scale ferrous metal material processing scenarios, electromagnetic cranes can achieve 30%~40% operation rhythm speed increase, which can offset their high initial investment and power operation and maintenance costs within several years.

    Safety Considerations

    Both types of equipment are suitable for heavy industrial operation scenarios with high load and large tonnage, but there are obvious differences in their safe operation characteristics:

    • Electromagnetic crane relies on continuous power supply to produce adsorption force to fix the load, so it must be equipped with a power failure and load maintenance system with standby energy storage device.This configuration is the standard configuration of industrial-grade equipment and is a must in equipment selection and procurement. It cannot be omitted.
    • At the same time, the electromagnetic crane does not need manual auxiliary hanging hangers, which greatly reduces the frequency of operation of workers under lifting materials and dangerous areas, and effectively avoids the safety risks of manual hanging operations.
    • Grab crane relies on mechanical clamping force to fix materials, without relying on continuous power supply to stably carry loads, and power failure safety is better.However, it is necessary to regularly check the wear of the grab jaws to avoid potential safety hazards such as insufficient clamping force and material falling due to component wear.
    • Both types of equipment shall be designed to match the working level of the working conditions (A6~A8 level shall be selected for scrap yard and raw material handling scenarios), and shall be equipped with redundant braking system to meet the continuous operation safety requirements of high frequency and heavy load.

    How to Choose: A Decision Framework by Mill Zone

    Most steel mills will not configure a single type of crane for the whole plant, but according to the material characteristics and operating environment of each cross-workshop, the crane model is targeted to maximize adaptability and operating efficiency. The specific selection standards for each area are as follows:

    • Raw material storage yard: grab crane shall be selected.Non-ferrous metals and bulk materials loading and unloading operations, rely on mechanical clamping structure to complete, grab crane can perfectly adapt to this kind of materials grab, transfer needs.
    • Scrap storage yard: grab crane shall be selected.The material category in this area is complicated, and the versatility of multi-material adaptation of grab crane is more important than the operation frequency advantage of electromagnetic crane, which can meet the flexible loading and unloading of various scrap steel.
    • Melting workshop/foundry workshop: electromagnetic crane shall be selected.The materials in this area are mainly homogeneous ferrous metals. The electromagnetic crane can realize high-frequency sub-cycle operation, greatly improve the melting feeding efficiency and meet the continuous production requirements.
    • Continuous casting billet operation area: electromagnetic crane shall be selected.It can absorb high temperature billet stably, effectively avoid the damage caused by clamping equipment to the surface of high temperature steel, and ensure the forming quality of billet.
    • Billet storage area: grab crane or mechanical clamping crane shall be selected.The magnetic adsorption performance of normal temperature steel and coated steel is greatly attenuated, the clamping stability of electromagnetic crane is insufficient, and the mechanical gripping equipment is more reliable.
    • Rolling finishing span: electromagnetic crane is selected.Electromagnetic crane is the best choice for the repetitive transfer of steel coils and plates because of its speed and safety.
    • Outdoor storage and open space: grab crane is selected.The equipment has stronger weather resistance, can adapt to extreme outdoor environments such as high and low temperature, wind and rain, and the operation stability is not affected by climate temperature fluctuations.
    • Pre-selection requirements: before determining the crane model, it is necessary to accurately verify the exclusive operation parameters of the single-span workshop, including single lifting weight, single shift lifting times, ambient temperature range, operation span, etc.Crane type and load class must be customized according to single-span operation parameters, rather than applying uniform standards for the whole plant.

    Duty Class and Capacity Notes for Steel Mills

    Crane load class and model is equally important, directly determines the service life of equipment and production stability, the operation area level specifications are as follows:

    • Core material transfer areas such as scrap storage yard and raw material storage yard: whether electromagnetic crane or grab crane, A6~A7 load level equipment shall be configured, which can adapt to high-intensity and uninterrupted cyclic operation conditions for a long time.
    • Molten metal and ladle operation area: higher standard A7~A8 heavy-duty customized equipment shall be adopted, equipped with redundant braking protection system to ensure operation safety under high-risk conditions.This area is not suitable for conventional electromagnetic, grab accessories, need special ladle, casting crane operation.

    Common error warning: improper load class selection is a high-frequency problem of steel plant equipment configuration.Ordinary “heavy duty” cranes that are only suitable for intermittent operations cannot withstand high-frequency continuous operations in areas such as scrap yards, and are prone to excessive wear and tear of equipment, frequent failures, and greatly shortened service life.

    Conclusion

    At present, there is no best option to state which is better between electromagnetic crane and grab crane. The choice of system has to be determined based on various factors as material feature, handling process, work environment and production requirement, etc. Electromagnetic system is more desirable to use in smelting the pure ferromagnetic material, and grab system can be better for bulk, mixture or non-magnetic material. Now many steel plant and material flow facility are using both system to maximize the efficiency.

    What material is to be handled, frequencies of lifts, load design, environment in which the material is to be moved in and whether or not the system is to be automated should all be established before looking at the purchase of an automated system. A system that has been well designed and specified will be easier to operate, cheaper to maintain and be more cost effective over its life span.

    Henan Mine Crane is one of the professional manufacture for all electric. electromagnetic overhead crane and heavy duty industrial cranes equipment. We are experienced in designing and manufacturing electric and electromagnetic overhead crane, port crane, grab crane, gantry crane and electric hoist. We also supply other intelligent material handing systems for steel mill, power plant, mining, port and scrap recycling industries and heavy industries.

    Henan Mine CraneDiscuss your requirements ↗
  • Electric Wire Rope Hoist Selection Guide: Low Headroom vs. Standard Types

    Electric Wire Rope Hoist Selection Guide: Low Headroom vs. Standard Types

    Electric Wire Rope Hoist Selection Guide: Low Headroom vs. Standard Types

    Wire rope electric hoists are the core equipment of industrial hoisting scenarios, and are widely adapted to various heavy-duty operation scenarios such as factory production, material transfer, equipment maintenance, and port loading and unloading.In the selection of equipment procurement, most users only pay attention to the rated load of the hoist, but ignore the key core factor of the structure.

    The mainstream wire rope electric hoists on the market are divided into two types: low-clearance wire rope electric hoists and standard wire rope electric hoists.The adaptation scenarios, structural advantages, and cost systems of the two are significantly different.

    This article will compare the characteristics, applicable scenarios and selection points of the two equipment in an all-round way, and help factory managers, procurement engineers, and equipment operation and maintenance personnel to accurately select suitable hoisting equipment based on plant conditions, hoisting requirements, and budget standards.

    What Is an Electric Wire Rope Hoist?

    The wire rope electric hoist relies on electric drive to realize heavy-duty lifting and translation operations. The core operating logic is simple and mature: the motor transmits torque through the gearbox, drives the reel to rotate at a uniform speed, and drives the wire rope to wrap or loosen, so as to realize the lifting action of the hook and load.

    At the same time, the braking system can lock the load at the moment the equipment stops, eliminating the risk of heavy objects slipping; the upper and lower limit switches accurately limit the operating stroke of the hook to avoid damage to the equipment by over-range collisions; the operating trolley cooperates with the control system to achieve accurate horizontal movement of the load, and the whole system is stable in linkage and easy to control to meet the needs of industrial high-frequency hoisting.

    Core components

    The wire rope electric hoist is composed of multiple core components in collaboration, and each component performs its own duties to ensure the safe and stable operation of the equipment.:

    -Drive motor: The core power unit of the equipment can match the power and speed requirements of different working conditions, and the output power is stable and long-lasting, ensuring the long-term stable start-stop and continuous operation of the hoist.

    • Wire rope reel: equipped with precision special rope grooves, it can guide the wire rope to be wound in an orderly and neat manner, effectively eliminate problems such as messy rope, off-groove, abnormal wear, etc., and extend the service life of the wire rope.
    • Variable speed gearbox: responsible for power transmission and torque adjustment, accurately control the lifting and operating speed, adapt to various heavy-duty hoisting conditions, and improve the power transmission efficiency and operating stability of the whole machine.
    • Wire rope and hook components: The core load-bearing components are made of high-strength and wear-resistant wire rope with safety self-locking hooks, with strong carrying capacity and high safety factor, which guarantees the safety of heavy-duty hoisting operations in all directions.
    • Braking system: The core safety protection structure can achieve smooth deceleration, precise shutdown and load locking, adapt to conventional operation braking and instantaneous braking in emergency working conditions, and eliminate the risk of heavy objects slipping.
    • Limit switch: Intelligent travel protection device, which accurately defines the upper and lower operating limits of the hook, effectively avoids over-range collisions, equipment damage and safety accidents, and realizes standardized limit protection.
    • Running trolley: The whole machine walks smoothly and horizontally along the main beam of the crane, with smooth movement and accurate positioning, which can realize flexible transfer and precise alignment of workpieces, and is suitable for multi-point hoisting operations.
    • Electrical control system: integrated handle control, wireless remote control, frequency conversion speed control and other multi-function modules, accurate and convenient control, equipped with multiple electrical protection mechanisms to ensure the intelligent and safe operation of the equipment.
    • Overload protection device: real-time dynamic monitoring of the hoisting load, once the rated load is exceeded, automatic shutdown will be triggered immediately, avoiding the risk of overload operations from the source, and protecting the safety of equipment and personnel.

    Mainstream application scenarios

    Wire rope electric hoists have the advantages of strong carrying capacity, large lifting stroke, stable operation, and low failure rate. They can be adapted to normal hoisting operations under all working conditions such as light load, medium load, heavy load, and overweight, and are suitable for almost all industrial lifting scenarios.According to the application field, it can be divided into the following three categories:

    • General processing and maintenance scenarios: widely used in machining workshops, equipment maintenance bases, steel structure processing plants and other scenarios, used for workpiece assembly, equipment displacement, mold replacement, daily maintenance and hoisting, suitable for high-frequency, lightweight to medium-heavy-duty conventional operations.
    • Heavy industry and energy scenarios: it is suitable for harsh working conditions such as steel mills, power plants, and heavy industry manufacturing workshops. It can stably complete the hoisting and alignment of steel billets, components, and large-scale unit equipment. It is resistant to high temperature and continuous load, and is suitable for high-intensity continuous operation needs.
    • Logistics and infrastructure scenarios: it covers outdoor and storage conditions such as warehousing and logistics centers, construction sites, ports and terminals, and is responsible for material handling, cargo stacking, and building materials transshipment. It adapts to the needs of hoisting with changeable sites and large operating spans.

    What Is a Standard Electric Wire Rope Hoist?

    The standard type (conventional headroom type) wire rope electric hoist is a classic configuration in the industry. It adopts the traditional modular structure layout. The motor, gearbox, reel, and operating trolley are arranged in a conventional manner. The overall structure is regular and no special optimization design is required. It is the most versatile hoisting equipment.This type of hoist is installed under the main beam of the crane, and the overall structure occupies a large vertical clearance space, which has basic requirements for the height of the plant floor.

    Core advantage

    • Mature structure and stable operation: relying on decades of industrialization and application accumulation, the standard modular structure has been verified by long-term working conditions, with stable and reliable performance and low failure rate, which can meet the long-term and uninterrupted continuous hoisting operations of enterprises, and the equipment has higher fault tolerance.
    • Simple operation and maintenance, universal accessories: The whole machine adopts an open layout design, the structure is transparent, the disassembly and assembly are convenient, and the daily maintenance, maintenance and parts replacement process is simple.The core accessories are highly versatile and the market is well stocked, which can effectively shorten the downtime and maintenance time and reduce the cost of equipment operation and maintenance.
    • Full coverage of tonnage and wide adaptability: the load specification system is perfect, fully covering light, medium, heavy and even heavy-duty conditions of more than 50 tons, while supporting non-standard tonnage customization, which can be adapted to the conventional and special hoisting needs of most industries.
    • Outstanding cost performance and controllable landing cost: the structural design is simple and mature, no complex precision machining technology is required, the equipment procurement threshold is low, the installation and commissioning are simple, the late operation and maintenance investment is small, and the comprehensive economic benefits of the whole life cycle are excellent. It is suitable for standardized projects with controllable budgets.
    • Excellent compatibility, suitable for many types of models: it is extremely versatile and adaptable, and can seamlessly match mainstream cranes such as single-beam, double-beam, gantry, and cantilever cranes. It is suitable for all kinds of standardized hoisting conditions such as conventional workshops, open-air sites, warehousing and logistics, and the threshold for equipment adaptation is lower.

    Applicable scenarios

    With the core advantages of mature structure, simple operation and maintenance, high cost performance, and wide adaptability, the standard wire rope electric hoist focuses on standardized hoisting conditions without vertical space restrictions.Combined with the actual use requirements, the applicable scenarios can be clearly classified from the two dimensions of the attributes of the adapted working conditions and the typical application site:

    Adapt to working condition attributes

    • Sufficient plant space: the vertical clearance height of the workshop and site is sufficient, and there is no need to compress the lifting height of the equipment structure, and there is no floor height restriction problem.
    • Conventional hoisting requirements: mainly for medium and light conventional material hoisting, equipment assembly, and daily maintenance, without the need for extreme high-level hoisting operations.
    • Normalized and stable working conditions: the operating frequency is stable and the load is uniform, mainly continuous conventional operations and low-frequency heavy-duty operations, and there is no need for high-intensity extreme working conditions.
    • Refined budget control: the project prioritizes the comprehensive price ratio of equipment procurement, operation and maintenance, and pursues low-cost, high-stability landing solutions.
    • Simple operation and maintenance requirements: on-site maintenance equipment is easy to overhaul, accessories are universal, and maintenance time is short, which reduces equipment downtime and loss.

    Typical application site

    • Newly built standardized factories: mechanical processing workshops with regular layout and sufficient floor height, equipment manufacturing production lines, and hardware processing workshops.
    • Warehousing and logistics sites: storage centers with high-level standards and open spaces, material transfer bases, and finished product stacking workshops.
    • Outdoor construction sites: open-air construction sites, depots, and outdoor equipment hoisting sites, without floor height constraints.
    • Conventional maintenance stations: factory equipment maintenance area, auxiliary hoisting stations, used for daily equipment disassembly, displacement, and maintenance operations.

    Overall, in the standardized working conditions without vertical space constraints, the standard wire rope electric hoist can give full play to the core advantages of stability and durability, wide adaptability, and low cost of operation and maintenance. It is the preferred equipment for industrial general hoisting scenarios.

    What Is a Low-Headroom Electric Wire Rope Hoist?

    The low-clearance wire rope electric hoist is a special equipment optimized for scenarios where the floor height of the plant is insufficient and the vertical clearance is limited.By reconstructing the equipment structure, optimizing the combined layout of the reel, motor, and trolley, and adopting a compact C-shaped structure design, the vertical spacing between the hoist body and the main beam of the crane is greatly reduced, and the headroom height occupied by the equipment itself is minimized.

    Core design principles

    Compared with the standard hoist, the low-headroom model re-optimizes the structure ratio of the whole machine, adjusts the installation position of the core components, and greatly shortens the vertical distance from the bottom of the main beam to the highest point of the hook (the hook is close).Under the premise that the total height of the plant is fixed, the effective lifting height of 200-500mm can be effectively increased, which perfectly solves the pain points of the traditional gourd industry of “enough space and insufficient lifting height”.

    Core advantage

    • The ultimate release of vertical space, greater lifting height: By optimizing the compact structure layout, the headroom occupied by the equipment itself is greatly reduced. Under the premise that the floor height of the plant is fixed, compared with the standard hoist, the effective lifting height can be increased by 200-500mm, and the potential of vertical working space can be fully tapped.
    • Strong space adaptability and double utilization rate: completely improve the pain points of traditional hoist fuselage squeezing vertical working space, perfectly adapt to the layout of modern workshops with dense equipment and compact workstations, and improve the overall space utilization rate of the plant in all directions.
    • Adapt to old-fashioned transformation, low transformation cost: there is no need to dismantle the factory building, raise the roof, and transform the main structure. It can be directly adapted to the upgrading and replacement of old cranes and equipment renovation projects. The construction cycle is short, the transformation investment is small, and the landing efficiency is high.
    • Optimize infrastructure design and save construction costs: For new plant projects, the design standards for plant floor height can be reduced, steel structure, enclosure, hvac and other infrastructure investments can be effectively reduced, and the total cost of project construction can be compressed from the source.

    Typical application site

    • Old and low-rise factories: old-fashioned processing workshops, assembly workshops, and hardware manufacturing buildings with long construction years, high and low floors, and insufficient clearance.
    • Equipment-intensive workshop: A modern intelligent manufacturing workshop with intensive automated production lines, compact layout of large machine tools, and tight vertical space.
    • Renovation and renovation project sites: various industrial workshops for the replacement of old cranes, the upgrading of hoisting systems, and the process transformation of the factory area.
    • Special restricted sites: production and storage areas where the top is covered with pipelines, bridges, and hvac equipment, and the effective operating floor height is further compressed.
    • Low-cost new factories: new standardized factories that adopt low-rise and high-infrastructure design, pursue high space utilization, and strictly control civil construction costs.

    Overall, the low-clearance wire rope electric hoist is specially tailored for space-constrained working conditions. Without changing the main structure of the plant, it maximizes the excavation of vertical working space and improves the hoisting height and site utilization. It is the optimal solution for industrial hoisting in restricted space.

    Low-Headroom vs. Standard Electric Wire Rope Hoists

    In order to facilitate users to visually distinguish the differences between the two devices, combining the core dimensions of structure, performance, cost, and adaptation scenarios, the precise comparison table is as follows:

    Contrast dimension Low headroom wire rope electric hoist Standard wire rope electric hoist
    Required plant clearance Extremely low, suitable for small vertical spaces Higher, sufficient layer height support is required
    Effective lifting height The same layer is higher and higher, lifting 200-500mm Limited by the structure of the equipment, the lifting height is limited
    Structural design Compact, integrated, optimized design, precise structure Traditional modular conventional structure, mature design
    Installation space requirements Adapt to small spaces, flexible installation Sufficient vertical installation clearance needs to be reserved
    Initial procurement cost High, the precision structure and process cost are higher Affordable and more cost-effective
    Maintenance difficulty The layout of the components is compact and requires professional maintenance and operation Open structure, simple and convenient daily maintenance
    Space utilization Excellent, maximize the value of plant space Good, completely enough when there is no space limit
    Best application scenario Low-rise factory buildings, old-fashioned renovation, space-restricted working conditions Standard factory building, adequate floor height, budget-sensitive working conditions

    Core summary: There is no absolute difference between the two gourds, only the adaptation scenarios are different.The core basis for selection is: plant space size, actual hoisting height requirements, crane configuration and project budget.The space is limited, choose the low headroom type, and the general working conditions give priority to the standard type.

    7 Key Factors When Selecting an Electric Wire Rope Hoist

    Rated lifting load

    The rated load is the basis for selection, and the maximum lifting load of the equipment needs to be accurately calculated, including the total weight of the workpiece, tooling, spreader, etc.When selecting the type, it is strictly forbidden to select the type only according to the maximum load of the load, and it needs to be combined with the average daily hoisting load and the frequency of operation to make a comprehensive judgment.

    High-frequency heavy-duty operations need to match higher-specification loads and operating condition levels to avoid small cars pulling large vehicles, resulting in accelerated wear and tear of equipment and shortened life; low-frequency light-load operations do not need to be over-selected to avoid budget waste.

    Actual required lifting height

    It is necessary to accurately measure the maximum stroke of the hook required for the operation, and calculate the whole process from the lowest reclaiming point to the highest unloading point, while avoiding the influence of obstacles such as workshop equipment, operation platforms, storage shelves, and pipelines.

    In the scenario of restricted floor height, the standard hoist will take up a lot of vertical space due to its own structure, which can effectively raise the height, and the structural advantages of the low headroom hoist can perfectly compensate for this defect and ensure that the operating height is up to standard.

    Available headroom height of the plant

    Headroom height refers to the vertical distance from the bottom of the main beam of the crane to the obstacles (roof, pipes, lamps) on the top of the plant, which is the core hard index of selection.Among them, the proximity of the hook is the key parameter, that is, the distance from the bottom of the main beam to the highest point of the hook. The smaller the value, the greater the effective lifting height.The standard hoist hook has a large distance at close range, which can easily waste vertical space; the low headroom hoist greatly reduces this value and maximizes the release of working space.

    Job level and work system

    The operating frequency, load ratio, and running time of different operating conditions vary greatly, and the selection of FEM and ISO operating condition classification standards must be strictly followed.The core considerations include: the number of starts per hour, the average daily operating time, the average load to the rated load ratio, and the service life of the equipment design.

    For light-duty maintenance conditions and low-frequency operations, a low-condition hoist can be selected; for high-frequency and continuous heavy-duty operations of the production line, it must be matched with high-condition equipment such as M5-M7.Insufficient selection of working conditions will lead to frequent equipment failures and frequent downtime and maintenance, which will seriously affect production efficiency; excessive selection will cause waste of equipment resources.

    Crane type and trolley configuration

    The electric hoist must be perfectly adapted to the supporting crane, otherwise there will be problems such as inconsistent installation, stuck operation, and safety hazards.Mainstream adaptation models include: single-girder bridge crane, double-girder bridge crane, gantry crane, monorail crane system, etc.At the same time, it is necessary to distinguish between the top-mounted and bottom-mounted trolley structures, and combine the crane’s main beam specifications, wheel track, and track gauge selection to ensure that the hoist is compatible and matched with the structure of the whole machine.

    Lifting and operating speed

    The speed of the equipment directly determines the operating efficiency and hoisting accuracy.The single-speed hoist has a simple structure and low cost, and is suitable for ordinary material transfer; the two-speed hoist can realize fast and slow switching, taking into account operational efficiency and precise positioning;

    The frequency conversion speed control hoist supports stepless speed regulation, stable start and stop, accurate positioning, and is suitable for precision equipment assembly and high-precision hoisting scenarios.Users can flexibly choose according to the production rhythm and operation accuracy requirements.

    Operating environment conditions

    The operating environment directly determines the protection level and special configuration requirements of the hoist.Standard protection models can be selected for indoor conventional environments; outdoor, dust, humidity, high temperature, and corrosive working conditions need to be equipped with sealed motors, high IP protection levels, and anticorrosive coatings; explosion-proof wire rope electric hoists must be selected for flammable and explosive scenes, and the whole machine adopts an explosion-proof structure to eliminate safety hazards and adapt to special industries such as chemical industry, mining, oil and gas.

    When Should You Choose a Low-Headroom Hoist?

    Low-headroom wire rope electric hoist is the exclusive preferred equipment for vertical space-restricted working conditions. It can specifically solve the pain points of insufficient lifting height of traditional hoist, low space utilization rate, and high cost of plant transformation. It is suitable for the following types of restricted operating conditions:

    • Insufficient floor height and limited headroom of the workshop: The original vertical headroom height of the workshop is low, and the standard electric hoist cannot meet the effective lifting height required for production due to the large space occupied by the fuselage structure, making it difficult to install and put into operation normally.
    • Upgrading and transformation of old factories: refurbishment of old workshop equipment and replacement of old cranes. The main steel structure and roof of the plant cannot be removed and raised. It does not meet the conditions for civil construction transformation. It is necessary to rely on the optimization of the equipment structure to improve the operating performance.
    • Requirements for high-level hoisting operations: The production process has extremely high requirements for the lifting stroke of the hook, and it is necessary to maximize the vertical working space to meet the high-precision and high-stroke hoisting requirements such as high-level equipment assembly, high-level material stacking, and alignment of large workpieces.
    • The layout of workshop equipment is dense: the automation equipment and large machine tools in the factory area are tightly arranged, and there are many top pipes, bridges, and hvac facilities. The vertical working space is greatly compressed, and the lifting operation gap is narrow.
    • Strictly control the cost of infrastructure construction: The new plant project needs to optimize the architectural design, reduce the height of the plant floor, reduce the investment in steel structure, civil construction, and enclosure, and compress the overall infrastructure cost of the project from the source.

    When Is a Standard Electric Wire Rope Hoist the Better Choice?

    Under conventional hoisting conditions without vertical space constraints, the standard wire rope electric hoist has the core advantages of stable operation, easy operation and maintenance, and excellent cost performance, and has better adaptability. The following scenarios can be preferred for selection and use:

    • Sufficient floor height of the plant: The vertical clearance space of the workshop is fully filled, which can fully meet the installation conditions and operating clearance requirements of the standard hoist. There is no floor height restriction, and the equipment can be directly and stably put into operation.
    • Conventional hoisting requirements: Daily production hoisting operations have moderate requirements for vertical lifting stroke, and the rated lifting parameters of the standard hoist are fully adapted, without the need for ultra-high stroke and extreme high-level hoisting performance blessing.
    • Controllable project budget: the equipment procurement and landing budget are limited, focusing on the comprehensive price ratio, and the initial investment in the procurement, installation and commissioning of standard gourds is lower, which can accurately control the project construction cost.
    • Standardized new factory area: it is adapted to the new standardized factory building with a regular layout and a high floor height target, which can be perfectly matched with conventional crane equipment and fits the general hoisting and installation conditions.
    • Lightweight operation and maintenance requirements: Relying on the characteristics of universal standard hoist accessories, open structure, and convenient disassembly and assembly, the daily maintenance process can be greatly simplified, and the equipment downtime loss and long-term operation and maintenance costs can be effectively reduced.
    • Conventional operating conditions: the operating environment has no space constraints, high-precision alignment, extreme lifting and other special process requirements, focusing on stable, high-frequency, and normalized general material hoisting and equipment maintenance operations.

    Common Mistakes When Choosing an Electric Wire Rope Hoist

    Only select the type based on the rated load

    The rated load is only the basic threshold for the selection of electric hoists. The working condition level, effective lifting height, space adaptation accuracy, and operation speed regulation performance are also the core indicators that determine the landing effect and service life of the equipment.

    If you rely solely on tonnage selection, there will often be various problems such as equipment load reaching the standard, but insufficient adaptability to working conditions, inconsistent installation space, and substandard operating efficiency, which will eventually cause frequent equipment failures, downtime for repair and even long-term idleness, seriously affecting the normal operation of the production line.

    Ignore the close-range parameters of the hook

    The close distance of the hook is the core selection parameter that can easily be ignored, which directly determines the effective lifting height of the equipment and is related to the actual available stroke of the hoisting operation.If the selection and matching of this parameter is not correct, it will directly cause the loss of hundreds of millimeters of vertical working space, resulting in the actual lifting height of the equipment can not meet the standards, does not meet the production process requirements, and ultimately leads to a series of problems such as equipment return and rework, project construction period lag, etc., increasing additional landing costs.

    Inaccurate measurement of plant headroom

    The measurement of the headroom of the plant is a key part of the selection. If the occupied height of the top obstacles such as pipes, lamps, brackets, etc. is ignored, or the highest point of the hook is not used as a unified measurement reference, it is easy to produce data deviations and cause selection errors.After the equipment procurement is completed, there is a high probability that there will be insufficient installation space and the effective lifting height is not up to standard, resulting in additional high costs and construction period losses for equipment transformation and replacement of the whole machine.

    Blindly pursuing low-cost equipment

    The initial investment in low-cost equipment is low, but there are generally problems of rough craftsmanship, poor-quality accessories, insufficient working condition level, and high failure rate.Long-term use will produce high maintenance costs, downtime losses, and replacement costs, and the overall cost of use is much higher than that of compliance with high-quality equipment.The selection of models needs to consider the whole life cycle cost comprehensively, rather than simply looking at the purchase price.

    Ignore the operating condition level

    Inconsistent selection of working condition levels is the core cause of early aging of equipment and soaring failure rates.If you choose a low-condition electric hoist in a high-intensity operation scenario with high-frequency and heavy-duty loads, it will exacerbate the wear and aging of core components such as brakes, wire ropes, gearboxes, etc., resulting in frequent equipment failures and shutdowns, which will not only seriously delay production progress and cause loss of production capacity, but also breed major hoisting safety risks.

    Ignore crane equipment compatibility

    There are obvious differences in the wheel track, track gauge, body size and weight of the trolley of different types of electric hoists, and they must be accurately adapted to the parameters of the main beam of the crane.If the equipment compatibility is not up to standard, it is very prone to problems such as operation caton, force imbalance, and structural deformation, which will not only cause safety hazards, but also directly invalidate the original equipment warranty rights and interests.

    How to Calculate the Right Hoist Configuration

    Following the following standardized accounting process, the adapted electric hoist model and full set of configurations can be accurately matched, and various problems such as selection deviation, equipment mismatch, and working conditions can be avoided from the source, and the equipment can be accurately landed.:

    1. Approved maximum hoisting load: accurately count the overall total weight of workpieces, spreaders, and tooling aids, and combine the daily average load and peak load to determine the rated load specifications required by the equipment to eliminate the problems of high configuration for small loads and low configuration for large loads.
    2. Accounting for effective lifting height: on-site measurement of the maximum operating stroke of the hook throughout the operation, covering the whole process of low-level reclaiming to high-level unloading, while avoiding interference from obstacles such as on-site equipment, shelves, pipelines, etc., to ensure that the actual operating height is sufficient.
    3. Accurately measure the headroom of the plant: Based on the bottom of the main beam of the crane, the vertical distance to the top obstacles such as the roof, pipes, lamps, etc. of the plant is accurately calculated, and the real and available vertical headroom parameters of the plant are obtained.
    4. Check the close-range parameters of the hook: Compare the manufacturer’s official equipment parameter table to verify the close-range value of the hoist hook, and combine the measured headroom size of the plant to verify whether the actual available lifting space of the equipment meets the production needs.
    5. Determine the operating conditions of the equipment: according to the core indicators such as the average daily operating time of the equipment, the frequency of start and stop per hour, and the load ratio, match the corresponding FEM and ISO operating conditions, and adapt to the intensity of various types of light, medium and heavy-duty operations.
    6. Matching and adapting operating speed: combining the operating efficiency of the production line with the requirements of workpiece hoisting accuracy, flexible selection of single-speed, two-speed or frequency conversion speed control configurations, taking into account the efficiency of hoisting operations and the stability of precise alignment.
    7. Check the on-site power supply conditions: check the on-site power supply voltage, frequency, power supply standard and other electrical parameters to ensure that the electrical configuration of the equipment is perfectly adapted to the on-site power supply system to avoid electrical adaptation failures.
    8. Verify the compatibility performance of the whole machine: check the wheel track, track gauge, fuselage size and other parameters of the electric hoist to accurately match the specifications of the crane’s main beam and operating track to ensure that the equipment is installed and runs smoothly.
    9. Evaluate the on-site operating environment: according to the on-site temperature and humidity, dust concentration, moisture corrosion, flammable and explosive working conditions, select the corresponding protection level, anti-corrosion, explosion-proof and other special configurations.
    10. Verification of compliance with industry standards: Ensure that the selected equipment fully complies with international industry safety design standards such as ISO and FEM, meets industrial hoisting safety specifications, and ensures the compliance and stable operation of the equipment.

    Core selection criteria: If the required clearance height of the standard wire rope electric hoist is greater than the actual vertical clearance available in the plant, it needs to be directly replaced with a low clearance hoist to make up for the lack of space and ensure that the lifting height of the equipment meets the standards and is put into operation normally.

    Conclusion

    The low-clearance type and the standard wire rope electric hoist have their own strengths, and the core of the selection is to match the plant space and hoisting conditions.The standard type is stable, easy to operate and maintain, and cost-effective, and is suitable for general hoisting of conventional factories; the low-clearance type has a compact structure and is suitable for restricted working conditions with insufficient floor height, renovation of old workshops and high lifting requirements.

    Enterprises should not only look at the price in the selection of models. They need to integrate the headroom height, lifting parameters, load, working level and operating environment, and rely on accurate parameter accounting to match the model, avoid adaptation errors and transformation costs, and effectively improve the efficiency of the whole cycle of equipment use.

    Henan Mine Crane, a professional lifting equipment manufacturer, can provide overall solutions for standard and low-clearance wire rope electric hoists and supporting lifting equipment. It can customize the adaptation configuration and engineering solutions according to the actual parameters of the project, and provide safe, efficient and adaptable equipment support for various industrial hoisting scenarios.

    Henan Mine CraneDiscuss your requirements ↗
  • Egypt Port and Logistics Crane Supplier | Reliable Port Equipment Solution

    Egypt Port and Logistics Crane Supplier | Reliable Port Equipment Solution

    Egypt Port and Logistics Crane Supplier | Reliable Port Equipment Solution

    Coastal ports in Egypt face salt spray corrosion and high-temperature exposure, while inland logistics yards suffer frequent sand and dust. These harsh local environments make standard industrial cables more costly than low upfront prices. These harsh environments make standard industrial cranes unable to sustain long-term stable operation in port and logistics scenarios.

    Egyptian port and logistics buyers now prioritize practical project adaptability and full lifecycle stability over simple budget costs. This article focuses on practical selection standards, key selection criteria, and the need for a comprehensive and cost-effective solution. focuses on practical selection standards, key technical parameters, supplier evaluation methods and common purchasing mistakes to help you find the This article focuses on practical selection standards, key technical parameters, supplier evaluation methods and common purchasing mistakes to help you find the most matched crane solution for local Egypt projects.

    Which projects in Egypt need Port Logistics Cranes?

    Specialized container terminals

    Egypt’s major container ports are responsible for a large number of import, export and transit container business, Port Said East Port, Alexandria New Port and other modern container hubs, handling thousands of standard containers per day. Shore bridges are responsible for ship loading and unloading, yard bridges are responsible for yard stacking and transshipment, and the whole set of equipment system directly determines the container throughput capacity of the terminal.

    This type of project requires high operational efficiency, continuous operation capability and automation level of the equipment, which is the core service scenario of Egypt port crane supplier.

    General Bulk Cargo Ports

    Traditional ports such as Alexandria Old Port and Port Said West Port Area are dominated by bulk cargo handling such as steel, engineering equipment, building materials and agricultural products. Flexible equipment such as gantry cranes and mobile harbor cranes are needed to meet the lifting needs of different types and sizes of cargo.

    This type of port operation category miscellaneous, cargo form of large differences in the generality and flexibility of the Crane is more demanding.

    Industrial and bulk cargo specialized terminals

    Egypt’s port industrial zones supporting a large number of specialized industrial terminals, mainly serving the petrochemical, steel, cement, energy and other industries. Responsible for raw materials into the factory, finished products outbound, large industrial equipment lifting and other operations, requiring large-tonnage, heavy-duty port cranes.

    This type of project on the equipment load margin, structural strength and stability requirements are stringent, must use industrial-grade heavy-duty models.

    Inland dry port and logistics hub

    With the improvement of Egypt’s inland logistics network, a number of large inland dry ports and integrated logistics hubs have been built around Cairo, the Suez Canal economic zone, and near the new administrative capital. These sites are mainly responsible for temporary storage of goods, distribution, transshipment, container dismantling and consolidation business, and a large number of gantry cranes and Overhead Cranes are used to complete the yard and warehousing operations.

    Inland logistics hubs have wide open spaces and high operating frequency, requiring equipment with good operational stability and low maintenance costs.

    Warehousing and Supporting Operation Area

    Port and logistics parks supporting warehouses, maintenance workshops, equipment storage areas, the need for small and medium-sized lifting equipment to assist material handling, equipment maintenance, tool storage. This type of scenario mostly uses single girder, double girder Overhead Cranes or small gantry cranes, which are suitable for light and medium loads, and normalized operation requirements.

    Henan Mine Crane manufactured Automated Container Gantry Crane

    Henan Mine Crane manufactured Automated Container Gantry Crane

    Common Procurement Requirements in Egyptian Port Logistics Industry

    Heavy-duty outdoor continuous operation capability

    Egyptian ports and logistics parks generally use two or three shifts of uninterrupted operation mode, Crane daily operating hours up to 16-20 hours. The equipment needs to withstand high-frequency, large load cyclic operation for a long time, ordinary industrial light-duty models are completely unable to adapt to this high-intensity working conditions.

    The purchaser will focus on the working level, structural strength and durability of the core components of the equipment to ensure that the equipment can maintain stable operation under continuous operation.

    Stringent anti-corrosion protection requirements

    Egypt’s ports along the Mediterranean and Red Sea coasts are subject to marine salt spray erosion all year round, and the high salt content of the air is extremely corrosive to the steel structure and metal parts. Ordinary industrial painting process, 1-2 years will appear paint peeling, steel structure corrosion problems, seriously affecting the service life of the equipment.

    All coastal port projects require Crane to adopt multi-layer marine heavy-duty anti-corrosion coating system, and key components are galvanized or passivated to resist salt spray corrosion.

    Suitable for high temperature and sandy environment

    Extreme summer temperatures in Egypt can reach more than 40 ℃, open-air equipment for a long time in the sun, the electrical system, hydraulic system, rubber parts are easy to overheat and aging. Inland and desert neighboring logistics parks, dusty weather is frequent, fine sand and dust is easy to invade the equipment running parts and electrical cabinets, resulting in wear and tear, jamming and circuit failure.

    The equipment needs to be equipped with high-temperature-resistant electrical components, heat dissipation optimized structure and fully sealed dustproof design to adapt to the harsh local climate conditions.

    Stable and Reliable Electrical Control System

    Some areas in Egypt have poor grid stability and frequent voltage fluctuations. Crane electrical system needs to have good voltage adaptability and anti-interference ability, to avoid equipment downtime or failure due to voltage fluctuations.

    At the same time, the control system should be simple to operate, easy to maintain, adapt to the technical level of local operators, reduce the difficulty of later use and maintenance.

    Perfect after-sales and parts supply

    The local industrial parts supply chain in Egypt is not perfect, and the procurement cycle of niche brands and customized parts is long and costly. Once the equipment fails, the untimely supply of spare parts will lead to a long downtime, resulting in huge economic losses.

    Purchasers prioritize suppliers that can provide fast technical response, stock commonly used wearing parts, and support cross-border parts supply.

    Flexible and customized solutions

    Cargo types, site layouts, and operational processes vary greatly from port to port and logistics project to logistics project. Standardized universal equipment is difficult to fully adapt to all scenarios, requiring suppliers to customize the equipment span, reach, lifting height, spreader type and control system according to the actual needs of the project.

    Recommended Crane Types for Egypt Port Logistics Projects

    Shore Bridge Container Crane (STS)

    Shore bridge is the core equipment at the berth front of container terminals, specializing in the loading and unloading operations of ocean-going container ships. With large outreach, high lifting height and high operating speed, it can be adapted to meet the needs of large container ships docking operations.

    Newly built modern container terminals in Egypt are generally equipped with large tonnage, automated shore bridges to enhance the efficiency of ship loading and unloading.

    Ship-to-Shore Crane manufactured by Henan Mine Crane,

    Tire-type Gantry Crane (RTG)

    The core scenario served by RTG crane supplier Egypt is container yard operation. The tire yard bridge does not need to lay a fixed track, mobile and flexible, strong site adaptability, and can be freely adjusted to the operating area according to operational requirements.

    It is suitable for container yards and inland dry ports with flexible layout and large fluctuation in operation volume, and is the most widely used type of yard crane in Egypt.

    Successful shipment from Henan Mine Crane Factory supply of containerized straddle car project

    Rail Mounted Gantry Crane (RMG)

    RMG crane supplier Egypt main standardized, automated container yard. The rail yard bridge runs along the fixed rail, with high positioning accuracy, good running stability, higher operating frequency, and can be docked to semi-automated and fully automated terminal control system.

    It is suitable for new large-scale standardized container terminals and intelligent logistics parks to realize high-density and high-efficiency yard operations.

    RMG Crane

    Gantry Harbor Cranes

    Gantry Cranes have a solid structure and a large operating range, and can be adapted to the loading and unloading of a variety of cargoes, such as steel, equipment, bulk cargoes and so on. They are widely used in Egypt’s traditional general-purpose ports, industrial terminals and bulk cargo ports.

    This type of equipment is highly versatile and can be used to meet diversified cargo lifting needs by replacing different spreaders.


    Mobile Harbor Cranes

    Mobile harbor cranes do not require a fixed installation base, and can quickly switch between operating berths and areas. It is suitable for multi-purpose terminals, temporary work sites, small and medium-sized ports, and can flexibly respond to the loading and unloading needs of different types of cargo.

    For small and medium-sized Egyptian ports with unstable workload and changing cargo types, mobile harbor cranes are a cost-effective choice.

    Specialized Bridge and Gantry Cranes for Logistics Zones

    Inland logistics hubs, warehousing parks and ancillary workshops, mostly use single-girder and double-girder Overhead Cranes and Gantry Cranes. Responsible for cargo stacking, pallet transfer, equipment maintenance and other operations, suitable for light and medium load, normalized logistics scenarios.

    This type of equipment is simple in structure, convenient in maintenance and low in operation cost, and it is the standard equipment in the logistics supporting area.

    Core technical parameters to be confirmed by the purchaser

    Rated lifting capacity

    Lifting capacity selection needs to consider the maximum weight of goods, spreader weight and safety margin. Container operation should be calculated according to the weight of fully loaded container plus spreader, while bulk cargo and industrial equipment operation should be determined according to the maximum load of a single piece, and full load long-term operation is strictly prohibited.

    Outreach and span

    The outreach of the quay bridge should match the width and draught depth of the docking ship to ensure that it covers the whole operating range of the ship. The span of the yard bridge should match the standard partition width of the yard, and the operation radius of the gantry crane and mobile harbor crane should cover the operation area of the berth and the yard.

    Lifting height

    The lifting height needs to take into account the ship’s deck height, the number of container stacking layers, and the safety headroom of cargo lifting. At the same time, it should take into account the tide difference along the Egyptian coast to ensure that loading and unloading operations can be carried out normally at both high and low tides.

    Running length

    The running length of the truck determines the operation coverage of the equipment, which needs to match the length of the quay berth, the overall layout of the yard and the logistics operation line to ensure that there is no dead angle in the whole area.

    Working Level

    Port and logistics projects are mostly high-frequency continuous operations, and must use medium-heavy duty and above working level equipment. The core operation area needs to use heavy-duty working level to avoid equipment aging in advance due to long-term overload operation.

    Operating speed parameters

    The lifting speed, trolley running speed and trolley traveling speed directly affect the operation efficiency of the terminal and yard. According to the demand of project throughput, it is necessary to reasonably match the speed parameters to balance the operational efficiency and smoothness of operation.

    Maneuvering mode

    Traditional terminals can use cab control or wireless remote control, while new automated terminals can be equipped with semi-automatic or fully automatic control systems. The control mode should match the automation level of the project and the technical ability of the operators.

    Environmental protection requirements

    Coastal projects need to specify the level of marine heavy corrosion protection, inland dusty areas need to specify the level of dustproof sealing, high temperature areas need to specify the requirements of high temperature resistance, to ensure that the equipment is suitable for the local environmental conditions.

    Power supply conditions

    Egypt’s industrial electricity standard is 380V/50Hz, and the electrical system of the equipment should be fully adapted to the local power supply parameters. Some remote areas have unstable power supply, manufacturers can be required to provide voltage stabilization and protection devices.

    Henan Mine Crane manufactured Automated Container Gantry Crane

    Henan Mine Crane manufactured Automated Container Gantry Crane

    How to select the right Egyptian port logistics Crane suppliers

    Confirm whether it is the source manufacturer

    Purchasers should first verify whether the supplier has independent harbor crane research and development, production and assembly capabilities, rather than a mere trade intermediary. The source manufacturer can control the welding process, structural quality, anti-corrosion standards and the quality of core parts, to protect the quality of equipment from the source.

    Henan Mine Crane Industrial has a large exclusive production base for port lifting equipment, with a full range of port and logistics cranes with independent production capacity, full export qualifications, and can be batch customized to meet the Egyptian conditions of the special equipment.

    Verification of similar port logistics project experience

    Priority is given to suppliers with experience in Egypt and Middle East and Africa port projects. Manufacturers with local project experience are familiar with Egypt’s climatic conditions, operating habits, acceptance standards and import processes, and can optimize the equipment program to avoid the problem of incompatibility.

    Evaluate engineering support capability

    High-quality suppliers can provide customized solutions based on the terminal layout, yard drawings, operational requirements provided by the customer, free of charge to review site conditions, recommend the appropriate type and configuration of Crane. Instead of simply marketing standardized generic equipment.

    Verification of a full set of technical documents

    Regular export manufacturers can provide a complete set of technical data in English, including equipment assembly diagrams, technical parameter manuals, electrical schematic diagrams, load data, list of core components, factory quality inspection reports, operation and maintenance manuals. Meet the needs of customs clearance, acceptance, documentation and later operation and maintenance of Egyptian projects.

    Confirmation of core component brands and configurations

    Core components such as motor, reducer, brake, PLC control system, wire rope, spreader, etc. directly determine the operational stability and service life of the equipment. When purchasing, it is necessary to clarify the brand, specification and protection level of the components, and eliminate under-allocation and under-provisioning.

    Verify the quality control and factory inspection process

    Port Cranes belong to heavy-duty and high-risk equipment, and before leaving the factory, they must complete a full set of quality inspection processes, such as weld flaw detection, structural dimensional calibration, electrical system testing, no-load test run, full-load load test, overload test, and so on. Manufacturers are required to provide complete quality inspection records to ensure that the equipment has no hidden quality problems.

    Clarify the scope of installation and commissioning and services

    Confirm in advance whether the supplier provides equipment shipping, on-site installation guidance, machine commissioning, start-up acceptance and operator training services. Overseas port projects require high installation accuracy, and professional technical guidance can effectively avoid problems such as irregular installation and commissioning.

    Confirmation of warranty and after-sales parts support

    Clarify the warranty period, warranty coverage and after-sales response time. Priority should be given to suppliers that can provide remote technical support, stock commonly used wearing parts, and support cross-border fast parts supply to ensure stable operation of the equipment in the later stage.

    Henan Mine Crane manufactured Automated Container Gantry Crane

    Henan Mine Crane manufactured Automated Container Gantry Crane

    Common Misconceptions of Purchasers

    Blindly pursuing low prices is the top purchasing mistake. Low-cost cranes usually adopt lightweight structures, low-grade parts and basic anti- corrosion treatment, leading to frequent failures. Low-cost cranes usually adopt lightweight structures, low-grade parts and basic anti- corrosion treatment, leading to frequent failures and high maintenance costs in long-term port operation.

    Ignoring coastal salt spray corrosion and choosing standard industrial painting will cause steel rust and component aging, greatly shortening crane Ignoring coastal salt spray corrosion and choosing standard industrial painting will cause steel rust and component aging, greatly shortening crane service life in Egyptian port environments.

    Mismatching crane models with actual cargo types and working scenarios results in poor adaptability and frequent equipment breakdowns at port and logistics yards. Using light-duty cranes for continuous operation

    Using light-duty cranes for continuous heavy port operations causes structural fatigue and component damage, bringing potential safety risks.

    Focusing only on main equipment prices while ignoring installation, commissioning, training and spare parts leads to extra hidden costs and project delays. Incomplete project data in the project

    Incomplete project data in the quotation stage leads to mismatched design solutions, repeated modifications, cost overruns and delayed construction.

    Frequently Asked Questions

    What type of Crane is best suited for Egyptian port projects?

    Container terminal berth front selection of quay cranes, container yard preferred RTG tire type yard bridge, new automated terminals can be used RMG rail type yard bridge. General bulk terminals use gantry cranes or mobile harbor cranes, inland logistics hubs use gantry or Overhead Crane.

    How to choose between RTG and RMG?

    RTG tire cranes are preferred for projects that require flexible adjustment of operation areas and irregular yard layout. In pursuit of standardization, automation, high-density operation of large container terminals and intelligent logistics parks, priority is given to the use of RMG rail-mounted cranes.

    How important is anti-corrosion protection for coastal projects?

    Salt spray corrosion along the Egyptian coast is the biggest source of loss for port equipment. High-quality marine heavy-duty corrosion protection can extend the service life of the equipment by 2-3 times, significantly reduce the maintenance costs and the probability of failure, which is the basis for the long-term stable operation of port equipment.

    What are the core technical documents I need to ask for before placing an order?

    You need to ask for the assembly drawings, detailed technical parameters, electrical schematic diagrams, load data, list of brands of core components, a full set of factory quality inspection reports, and English operation and maintenance manuals.

    Can a supplier provide both terminal and inland logistics equipment?

    Professional scale crane manufacturers can provide a full range of equipment such as shore bridge, RTG, RMG, gantry crane, mobile harbor crane, Overhead Crane, gantry crane, etc. in one stop. Covering the whole scene of port handling, yard transfer, inland logistics, unified after-sales system to reduce docking costs.

    How important is after-sales service to port logistics Crane?

    Port and logistics project downtime losses are extremely high, a single day of downtime may cause tens of thousands or even hundreds of thousands of dollars in economic losses. Rapid troubleshooting, parts replenishment and technical maintenance services can minimize the length of downtime and protect the normal operation of the project.

    In addition to the price also need to focus on what to check?

    Focus on checking the working level of the equipment, anti-corrosion process standards, core component brands, factory testing process, installation and commissioning service scope, warranty terms and after-sales parts supply capacity. These factors directly determine the long-term value of the equipment and operating costs.

    Henan Mine Crane manufactured Automated Container Gantry Crane

    Henan Mine Crane manufactured Automated Container Gantry Crane

    Summary

    The core of selecting a reliable Egypt port and logistics crane supplier is not to find the lowest price, but to find a long-term partner who is suitable for the special working conditions in Egypt, matches the actual needs of the project, and can provide full-process support.

    Egypt port and logistics projects both coastal salt spray corrosion, high temperature and sunshine in summer, inland sand and dust frequent, continuous heavy-duty operation of the harsh characteristics of the crane design standards, manufacturing process and protection configuration requirements are much higher than ordinary industrial equipment. Only professional port equipment manufacturers can create durable equipment suitable for local working conditions.

    High-quality suppliers can not only provide high-quality lifting equipment, but also from the analysis of working conditions, program design, manufacturing, factory testing, cross-border delivery, installation and commissioning to after-sales maintenance, to provide a full range of professional services. To help purchasers avoid common misconceptions, reduce project risks and full life cycle operating costs.

    Henan Mine Crane Industrial has been deeply engaged in the Middle East and Africa port and logistics lifting market for many years, and is familiar with the climatic conditions, operational standards and import procedures of Egyptian ports and logistics parks. We can customize a full range of special cranes for ports and logistics, supporting marine heavy corrosion, high temperature, dust and wind special optimization, provide a full set of English compliance information and long-lasting cross-border after-sales protection.

    If you have Egyptian port or logistics crane procurement needs, you can send your lifting capacity, reach / span, lifting height, cargo type, yard / berth layout and project drawings, our technical team will recommend the appropriate crane solutions for you.
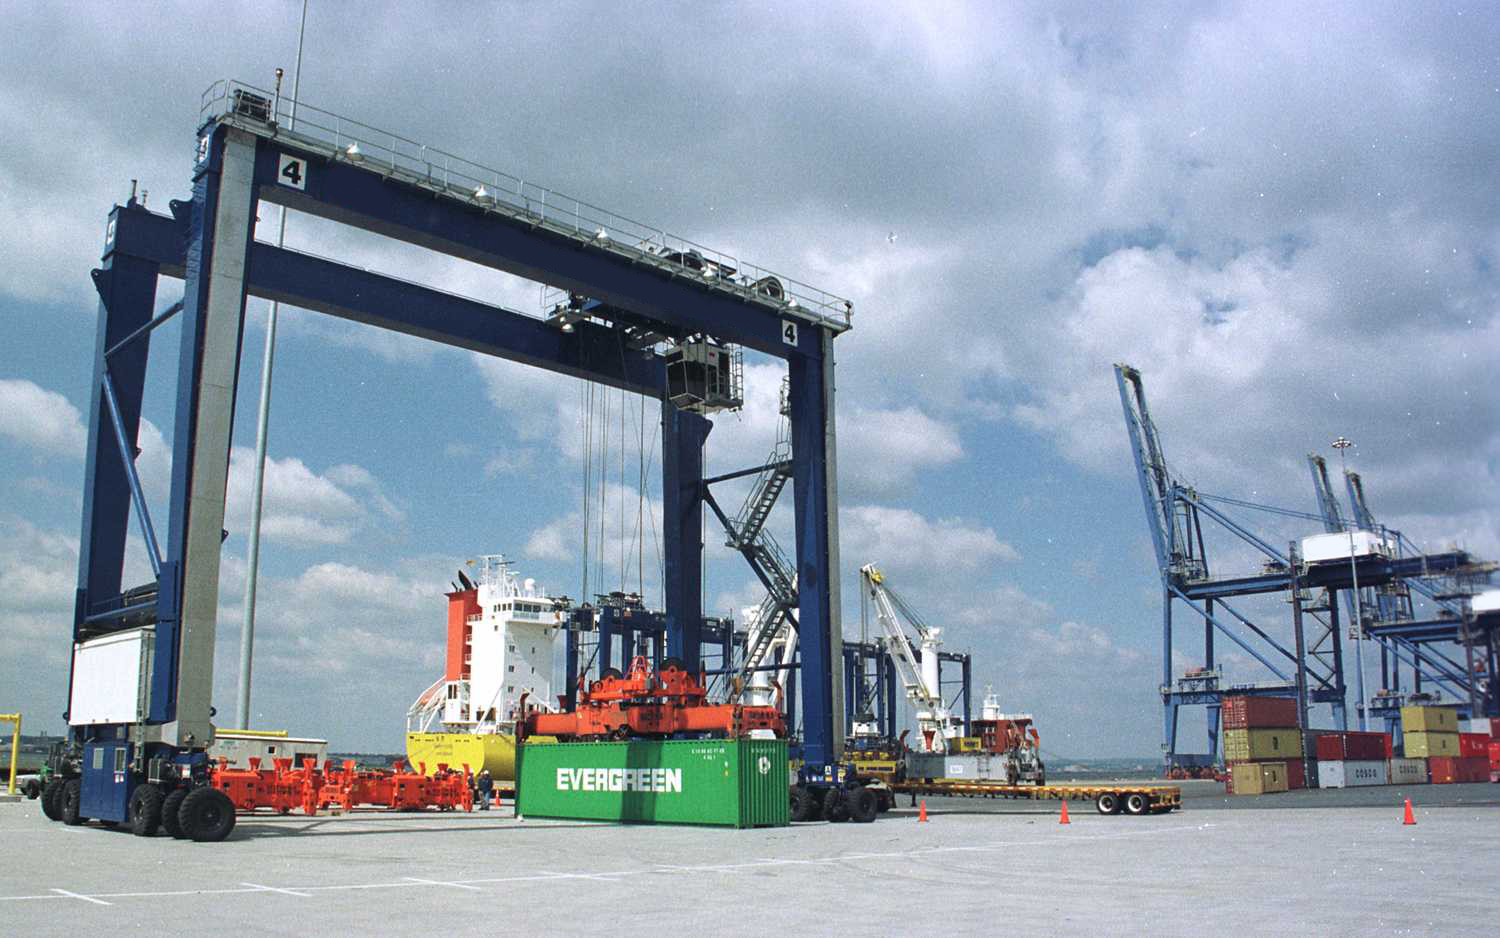
    Henan Mine CraneDiscuss your requirements ↗
  • Double Girder Overhead Crane Cost: Factory Direct vs. Local Dealer

    Double Girder Overhead Crane Cost: Factory Direct vs. Local Dealer

    Double Girder Overhead Crane Cost: Factory Direct vs. Local Dealer

    In the field of industrial lifting equipment procurement, the price difference of double-girder bridge cranes has always been the core issue that buyers are most concerned about.For double-girder bridge cranes of the same specifications, the quotation of different procurement channels may vary by 30% or more. This is not simply inflated pricing, but is affected by multiple factors such as product configuration, procurement model, and service system.For enterprises with lifting needs such as factories, workshops, logistics and warehousing, it is necessary to sort out the root causes of price differences in order to accurately control procurement costs and choose the procurement plan with the best price ratio.

    Double Girder Overhead Crane Cost Breakdown

    Price factors

    The basic pricing core of the Henan Mine Crane manufactured double-girder bridge crane is determined by the hardware configuration and technical parameters of the product itself, which is the core part of the cost composition.The first is the rated lifting weight. The larger the lifting weight, the higher the grade of core components such as the thickness of the main beam steel plate, motor power, and wire rope specifications required, and the cost will rise. For example, the cost of a 50-ton double-girder crane is much higher than that of a 10-ton model.The second is the span and lifting height. The larger the span, the higher the bending resistance of the main beam. Higher-quality steel and reinforced structural design are required, which directly increases material costs.The higher the lifting height, the corresponding increase in the length of the wire rope and the torque requirements of the motor.

    In addition, the level of work is also a key factor. High-level cranes (such as A6-A8) that operate frequently need to be equipped with more durable parts and frequency conversion control systems, and the cost is 15%-20% higher than ordinary working-level (A1-A3) models.Finally, brand differences in core components will also affect pricing. Models with imported motors, frequency converters, and brakes are usually 20%-30% higher in price than domestic models with high-quality components, but they have more advantages in performance and service life.

    Hidden costs

    When calculating costs, many buyers often only pay attention to the quotation of the equipment itself, but ignore many hidden costs, which eventually leads to actual expenditures far exceeding the budget.First, transportation costs. Double-girder bridge cranes are large-scale equipment. Transportation requires special vehicles and professional loading and unloading. The farther the distance and the larger the equipment, the higher the transportation costs. Some long-distance transportation also requires additional insurance costs, accounting for 5%-15% of the total equipment cost.

    Second, the cost of installation and commissioning. The crane is a special equipment. The installation requires a professional team to operate, and it also needs to cooperate with civil construction, track laying and other work. If the purchaser does not meet the relevant conditions, additional installation fees and civil renovation fees will be required. This part of the cost may be as high as tens of thousands of yuan.Third, the cost of acceptance and compliance, special equipment needs to be accepted by a professional testing agency before it can be put into use, and the cost of acceptance and qualification processing can easily be ignored.Fourth, the cost of late maintenance and spare parts, the supply price of spare parts and the cost of maintenance services in different procurement channels vary greatly. In the long run, this part of the hidden cost will directly affect the whole life cycle cost of the equipment.

    Factory Direct Double Girder Overhead Crane Cost

    Direct purchase benefits

    The factory direct supply model refers to the purchaser directly docking procurement with the crane manufacturer, eliminating intermediate links, and the core advantages are concentrated on cost and product control.First of all, the price advantage is significant. There is no intermediate price increase link for distributors. Buyers can purchase equipment at a price closer to the ex-factory price, which usually saves 10%-25% of the purchase cost. For large-volume purchases or large-scale crane purchases, the cost savings are more considerable.

    Secondly, product quality is more guaranteed. Buyers can directly connect with manufacturers to understand production processes and raw material procurement channels, and even go to the factory for on-site inspections to ensure that the equipment meets their own needs and quality standards, so as to avoid shoddy dealers.In addition, customized services are more flexible, and manufacturers can tailor equipment parameters according to the actual working conditions of the purchaser to meet individual use needs.Finally, the after-sales docking is more direct. When there is a quality problem or technical failure, the manufacturer’s technical team can be directly contacted without going through the dealer’s transit, and the response efficiency is higher.

    Direct purchase challenges

    Although the advantages of the factory direct supply model are obvious, there are also certain challenges, and buyers need to be prepared in advance.First, the early communication cost is high, and the purchaser needs to have certain professional knowledge and understand the technical parameters and selection criteria of the crane, otherwise it is prone to selection errors and affect the use effect.Second, it is difficult to coordinate transportation and installation. Manufacturers are usually only responsible for equipment production. Transportation, installation and other links require the purchaser to connect with third-party institutions on its own. Improper coordination may lead to delayed delivery of equipment, irregular installation and other problems.

    Third, the geographical restrictions are obvious. If the purchaser is far away from the manufacturer, the transportation cycle will be extended, and the response speed of on-site maintenance in the later stage may be affected, and some remote areas even need to pay additional on-site service fees.Fourth, the payment terms are relatively strict. Manufacturers usually require a certain percentage of the payment in advance. Some manufacturers may also require the full payment to be shipped after the account arrives, which has certain requirements for the purchaser’s financial liquidity.

    Local Dealer Double Girder Overhead Crane Cost

    Dealer pricing factors

    The pricing of local distributors is not simply the ex-factory price of the equipment, but the final quotation after combining multiple factors.First of all, the purchase cost of the dealer and the price of the dealer’s goods from the manufacturer are affected by the purchase volume and the cooperative relationship. The larger the purchase volume, the lower the price of the goods, and the quotation is relatively more advantageous.Secondly, for operating costs, local distributors are required to bear operating costs such as store rent, personnel wages, and storage costs. These costs will be apportioned to the quotation of each equipment.

    Third, service costs, dealers usually provide one-stop services such as transportation, installation, commissioning, and after-sales. These service costs will be included in the quotation system, especially the on-site service costs of local dealers are relatively low, and the service response is more timely.Fourth, the relationship between market supply and demand, if the local market has strong demand for double-girder bridge cranes, the dealer may appropriately increase the quotation.Conversely, in order to seize market share, certain discounts may be given.In addition, the brand positioning of the dealer will also affect the pricing. The quotation of the dealer acting for a well-known brand is usually higher than that of the dealer acting for an ordinary brand.

    Dealer advantages

    The core advantages of the local distributor model lie in convenience and service assurance, especially suitable for small and medium-sized enterprises that lack professional procurement teams and technical support.First, one-stop service saves worry and effort. Dealers usually provide full-process services from selection, quotation, transportation, installation to after-sales. Buyers do not need to connect multiple entities, greatly reducing communication and coordination costs.

    Second, the geographical advantages are obvious. Local distributors are closer to the purchaser, the transportation cycle is shorter, the equipment delivery speed is faster, and the late on-site maintenance and replacement of spare parts can also achieve rapid response, reducing the losses caused by equipment downtime.Third, the payment method is more flexible. Some distributors support payment in installments and cash on delivery to ease the financial pressure on buyers.Fourth, professional selection guidance, dealers are usually equipped with professional technical personnel, who can provide reasonable selection suggestions based on the actual working conditions of the purchaser, so as to avoid selection errors and reduce procurement risks.

    Factory Direct vs. Local Dealer Cost Comparison

    Initial price

    Judging from the initial purchase price, the factory direct supply model is generally lower than that of local distributors.Since the intermediate price increase link of the dealer is eliminated, the direct supply price is usually 10%-25% lower than the dealer’s quotation. For large-scale and high-configuration Henan Mine Crane manufactured double-girder bridge cranes, the price gap may be even greater.For example, for a 10-ton standard double-girder bridge crane with a span of 20 meters, the factory direct supply price may be 120,000-150,000 yuan, while the quotation from a local dealer may be 140,000-180,000 yuan.However, it should be noted that some distributors may drain through low prices, and charge additional fees for installation, spare parts, etc. In the later stage. Buyers need to carefully check the quotation details to avoid being misled by low prices.

    Service cost

    Service cost is one of the core differences between the two procurement models.Under the direct supply model of the factory, the basic after-sales service is usually provided by the manufacturer, but the purchaser shall bear the transportation, installation, commissioning and other services. If the manufacturer is required to provide on-site service, additional travel and labor costs will be paid. In the long run, the service cost may increase year by year.Local dealers usually include transportation, installation, commissioning and other services in the quotation. Some dealers will also provide free regular inspection and maintenance services. The supply price of spare parts in the later stage is relatively transparent. Although the initial quotation is higher, the long-term service cost is more controllable.Especially for companies that lack a professional maintenance team, the dealer’s one-stop service can effectively reduce late operating costs.

    Delivery time

    In terms of delivery time, local distributors have more advantages.Dealers usually reserve a certain amount of standard model inventory. After the purchaser places an order, transportation and installation can be quickly arranged. The delivery cycle is usually 7-15 days.In the factory direct supply mode, manufacturers need to arrange production according to the purchaser’s order. The production cycle is usually 15-30 days. In addition to the transportation time, the overall delivery cycle may be as long as 30-45 days. If the purchaser has urgent needs, it may affect the production schedule.However, for equipment with high customization requirements, although the production cycle directly supplied by the factory is long, it can better meet individual needs, while distributors usually only provide standard models, and the customization ability is relatively weak.

    How to Calculate Total Crane Cost

    Total ownership cost

    Accounting for the cost of Henan Mine Crane manufactured double-girder bridge cranes should not only focus on the initial purchase price, but should fully account for the total cost of ownership (TCO) throughout the life cycle, which is the core basis for judging the cost performance of the procurement plan.The total cost of ownership mainly includes four parts, one is the initial procurement cost, that is, the quotation of the equipment itself.The second is the cost of installation and commissioning, including transportation costs, installation costs, civil renovation costs, acceptance and compliance fees, etc.The third is the operation and maintenance costs, including electricity, lubricating oil, regular maintenance, spare parts replacement, etc., which usually account for 3%-5% of the original value of the equipment/year.The fourth is the cost of scrap disposal, that is, the cost of disassembly and disposal after the service life of the equipment expires.The purchaser needs to comprehensively account for these four parts of the cost and compare the total cost of ownership of different procurement models, rather than simply comparing the initial quotation.

    Supplier evaluation

    Choosing the right supplier is the key to controlling the total cost of ownership.The purchaser needs to evaluate the supplier from multiple dimensions. First, the qualification and strength, verify whether the supplier has the special equipment production/operation qualification, the manufacturer needs to have the corresponding production license, and the distributor needs to have formal agency authorization and business qualification.The second is product quality. Check the supplier’s product cases and customer evaluations to understand the performance, service life, failure rate, etc. of the equipment.The third is the service capability, which evaluates the supplier’s after-sales response speed, service coverage, spare parts supply capacity, and whether it can provide one-stop service.The fourth is price transparency, which requires suppliers to provide detailed quotation details, clarify the composition of various fees, and avoid hidden charges.The fifth is the reputation of cooperation. Through industry reputation and feedback from old customers, we can understand the integrity and cooperation experience of suppliers.

    When to Choose Factory Direct Purchase

    The factory direct supply model is suitable for buyers who meet the following conditions. First, they have a certain professional procurement knowledge and technical team, and can independently complete the selection, docking, transportation and installation links.The second is that the procurement scale is large, or customized equipment is required, and there are special requirements for product parameters and configuration.The third is to pursue the ultimate procurement cost control, and be able to accept long delivery cycles and relatively complex coordination processes.Fourth, the area is closer to the manufacturer, or has the ability to solve transportation, installation and other problems on its own, so as to reduce the service shortcomings caused by the region.For example, for large-scale production enterprises and factories with professional equipment management teams, choosing the factory direct supply model can minimize procurement costs while meeting individual use needs.

    When to Choose a Local Dealer

    The local distributor model is more suitable for the following buyers, one is the lack of professional procurement and technical teams, hoping to obtain one-stop service, worry-free and labor-saving.The second is that there is an urgent need for use, and the equipment needs to be delivered and installed quickly.Third, the area is far away from the manufacturer, transportation and on-site maintenance are inconvenient, and local service providers are required to provide a quick response.Fourth, the liquidity of funds is limited and flexible payment methods are required.Fifth, the late service requirements are high, and we hope to obtain stable and convenient maintenance and spare parts supply.For example, for small and medium-sized enterprises and project parties with temporary lifting needs, choosing a local distributor model can effectively reduce communication costs and operational risks, and ensure that the equipment is put into use quickly.

    Henan Mine Crane Factory Custom

    In summary, the procurement cost of double-girder bridge cranes is not a single quotation, but a comprehensive system covering product configuration, procurement model, hidden costs and full life cycle services.The factory direct supply model relies on the advantages of price and customization to adapt to buyers with professional capabilities, cost control and personalized needs.The local distributor model focuses on convenient service and rapid response. It is more suitable for buyers who lack a professional team and pay attention to delivery efficiency and post-service. Buyers need to calculate the total cost of ownership based on their own needs and choose suppliers on the best basis.

    As a professional large-scale crane manufacturer, Henan Mine Crane Factory directly supplies double-girder bridge cranes, eliminating the need for intermediate price increases, which can not only ensure product quality and customized needs, but also strictly control procurement costs.We have formal special equipment production qualifications, provide professional selection guidance and perfect after-sales guarantee, and can tailor equipment according to your working conditions to help enterprises carry out lifting operations efficiently and in compliance. Welcome to consult and connect.

    Henan Mine CraneDiscuss your requirements ↗
  • Different Types of Cranes and Their Industrial Applications

    Different Types of Cranes and Their Industrial Applications

    Different Types of Cranes and Their Industrial Applications

    Cranes are indispensable heavy lifting equipment in modern industrial production, building construction, port logistics and other fields. From small parts handling in the workshop, to container loading and unloading in the port, to the structure of high-rise buildings lifting, almost every scene that requires moving heavy objects, you can see the figure of the crane.

    Next, I will combine many years of front-line experience, the industrial field commonly used crane types, their respective characteristics, as well as the corresponding application scenarios, in layman’s terms to make it clear, to help you avoid the selection of misunderstandings.

    Henan Mine Crane Factory rail-mounted container gantry crane

    What Is an Industrial Crane?

    Basic Definition

    Industrial crane is a mechanical device used to lift and carry heavy objects, the core function is to realize the movement of heavy objects in the vertical and horizontal direction through the lifting mechanism. It is not as simple as an ordinary lifting tool, but consists of a complete set of mechanical and electrical systems that can stably and safely handle loads of different weights and specifications.

    Whether it is a few tons of small equipment or hundreds or thousands of tons of heavy components, as long as the right type of crane is selected, accurate handling can be achieved. Its core value is to replace manual handling and solve the problem of heavy materials that cannot be moved manually.

    Main Components of a Crane

    Regardless of the type of crane, the core components are inseparable from these four, understand these components, can help you better judge the quality and performance of the equipment.

    The hoisting mechanism is the “power core” of the crane, mainly composed of motor, drum, wire rope or chain, hook, responsible for lifting and lowering heavy objects, is to complete the lifting operation of the core execution parts.

    Structural frame or boom is the crane’s “skeleton”, used to support the hoisting mechanism and heavy loads, different types of cranes, structural frame varies greatly – some are the main beam structure, some are retractable boom.

    Operation system determines the crane’s mobility, some are fixed on the track operation, some are mounted on tires or crawler trucks, can move freely, adapted to different operating sites.

    The control system is the “brain” of the crane, divided into cab control and wireless remote control, responsible for issuing a variety of action commands, while integrating overload protection, limit protection and other safety features to ensure operational safety.

    Why Different Types of Cranes Exist

    Many people will ask, why do we need to design so many kinds of cranes? In fact, the answer is very simple, it is because of the different operating scenarios, the demand is too different, a crane can not meet all the working conditions.

    First of all, the load capacity is different, some operations only need to carry a few tons of heavy materials, some need to lift hundreds of tons of heavy components, such as shipbuilding, marine engineering, the crane’s load capacity requirements are extremely high.

    Secondly, the operating environment is different, some operate in closed plants with limited space; some operate in open-air construction sites and harbors, and need to cope with harsh environments such as rain and wind, salt spray, etc., which requires different protection and wind resistance of cranes.

    Mobile needs are also different, some operating sites are fixed, the crane does not need to move, as long as the coverage of the fixed area can be; some operating sites are scattered, the crane needs to be flexible and mobile, and even able to travel on complex roads.

    There are also differences in the scale of the project, small workshop maintenance and large infrastructure projects, the span of the crane, lifting height, operational efficiency requirements, but also completely different. It is these differences that give rise to different types of cranes, each adapted to different scenarios.

    Main Types of Cranes Used in Industry

     Overhead Cranes (Bridge Cranes)

    Key Features

    Overhead cranes, also known as bridge cranes, are the most common type of cranes used in industrial plants. Its core feature is that it is mounted on a railroad beam inside the plant, and the whole body is suspended under the roof without occupying ground space.

    Its operating range is mainly the entire span area of the plant, suitable for indoor material handling, smooth running, accurate positioning, and can cooperate with the production line to complete continuous operation. Because it is installed indoors, it is not affected by external weather and maintenance is relatively simple.

    Common Types

    Single girder overhead travelling crane, with simple structure, light weight and low manufacturing cost, the lifting capacity is generally 5-30 tons, which is suitable for light and medium-sized load workshop operation, such as parts handling in machining factories and small equipment installation.

    Double Main Girder Overhead Cranes, with two main girders, have greater rigidity and stronger load carrying capacity, with a lifting capacity of 30-500 tons, suitable for heavy-duty operations, such as steel billet handling in steel mills, and assembly of large equipment.

    Suspension overhead travelling crane, the main girder is suspended under the roof frame of the plant, no need to lay extra track beams, saving the space of the plant, suitable for small workshops with limited space, the lifting capacity is relatively small, generally in the range of 5-10 tons.

    Typical Industrial Applications

    Manufacturing factories are the main application scenarios of overhead travelling crane, such as automobile factories, machinery factories, which are used to carry parts and semi-finished products on production lines, connecting various production processes and reducing the secondary backward transportation of materials.

    Iron and steel factories are also the core application fields of overhead travelling crane, from smelting and rolling of steel billets to handling and stacking of finished steel products, all of them need to cooperate with overhead travelling cranes, especially the double main beam model, which can cope with the lifting demand of heavy steel billets.

    In large warehouses and logistics centers, when heavy goods need to be handled and the floor space is limited, overhead travelling cranes are the ideal choice, which can operate on the top of the warehouse without interfering with the stacking of goods on the ground and the passage of people.

    360t Foundry Crane factory

    Henan Mine Crane Factory 360t Foundry Crane

     Gantry Cranes

    Key Features

    The biggest difference between gantry cranes and overhead travelling cranes is that they have independent outriggers, which do not need to be attached to plant buildings, and the bottom of the outriggers are equipped with travelling devices, so that they can be operated on the ground track or on the level ground.

    Its biggest advantage is that it is suitable for outdoor operation, with large span and wide working range, and can cover the whole open field, such as harbor, yard, prefabrication yard, without large-scale modification of the existing site, and flexible installation.

    Main Variants

    Rail Mounted Gantry Crane (RMG), running on the ground laid track, with a fixed moving track, high positioning accuracy and large lifting capacity, is suitable for container terminals and large yards, and can realize high-density stockpiling and high-efficiency transshipment of goods.

    Tire Gantry Crane (RTG), using rubber tires as the walking device, do not need to lay tracks, can move freely on the level ground, great flexibility, suitable for small and medium-sized ports, temporary yards, can be quickly deployed for operations.

    Portable gantry cranes, miniaturized, detachable design, lifting capacity of 5-10 tons, span and lifting height can be flexibly adjusted, suitable for workshop maintenance, temporary lifting operations, can be easily transported after disassembly.

    Industrial Applications

    Container ports and terminals are the core application scenarios of gantry cranes. RMG and RTG are used in conjunction with each other to complete the loading and unloading of containers, stacking and storage, and connecting the port with the land logistics transfer, which is the core equipment for port operations.

    Shipyards are also inseparable from the gantry crane, especially large shipyards, need to lift hundreds of tons of gantry cranes, used to lift the hull segments, engines and other heavy parts, to ensure the accuracy of the hull assembly.

    Precast concrete yard, gantry cranes are responsible for handling prefabricated beams, prefabricated panels, prefabricated columns and other components, the characteristics of the outdoor open-air operation, just to match the layout of the prefabrication yard, can flexibly connect the production line and the yard.

    MC Electromagnetic Gantry Crane for sale

    MC Electromagnetic Gantry Crane

     Jib Cranes

    Structure and Design

    The structure of Jib Crane is very characteristic, which consists of a horizontal jib and a vertical column, the jib can rotate around the column (usually the rotation angle is 180-360 degrees), and the hoisting mechanism is mounted on the jib, which can realize accurate lifting in a small range.

    Its relatively small size, does not occupy a large area of space, suitable for fixed station lifting operations, simple operation, one person can complete the operation, mainly used for small tonnage, small range of material handling.

    Common Types

    Wall-mounted jib cranes, installed directly on the wall of the plant, without the need for independent columns, saving the ground and roof space, suitable for fixed workstations in the workshop, such as machine tools next to the parts handling, equipment maintenance.

    Floor-mounted jib cranes, with independent columns, fixed to the ground, with a larger swivel range, slightly larger lifting capacity than wall-mounted, suitable for workstations in the middle of the workshop, can cover multiple operating points.

    Articulated Jib Cranes, the jib can be folded, telescopic, more flexible, can bypass obstacles, suitable for complex working conditions, such as narrow space lifting, irregular material handling.

    Applications

    Workshop workstations are the main application scenarios of jib cranes, such as machining workshop machine tools, used to carry processed parts, without the need for frequent mobilization of large cranes, to enhance the efficiency of workstation operations.

    Assembly production lines are also commonly used jib cranes, especially the assembly of small parts, jib cranes can accurately send the parts to the assembly station, reduce manual handling, reduce labor intensity.

    Jib cranes can also play a role in equipment maintenance operations, such as workshop equipment dismantling, repair, lifting small parts or equipment components, flexible operation, without affecting the normal operation of the surrounding equipment.

    Mobile Cranes

    Key Characteristics

    The core feature of mobile cranes is strong mobility, can be flexibly transferred between different sites, without the need for fixed installation, can be quickly deployed to the scene of operation, suitable for temporary lifting, field operations or strong mobility conditions.

    Its telescopic and luffing boom can adjust the lifting height and working radius according to the operational requirements, which is suitable for different lifting scenarios, from light lifting to heavy lifting.

    Shipyard Gantry Cranes (Goliath Cranes)

    Special Characteristics

    Shipyard Gantry Cranes, also known as Giant Gantry Cranes (Goliath Cranes), are heavy-duty cranes specially designed for the shipbuilding industry, and are characterized by their large span and extremely high lifting capacity.

    Its span is usually 50-100 meters, can cover the entire dry dock, the lifting capacity can be up to 500-1000 tons or more, can lift dozens of meters long, hundreds of tons of hull segments, the accuracy requirements are extremely high.

    Because shipyards are mostly located in coastal areas, these cranes also have strong wind resistance and corrosion resistance, and can cope with coastal salt spray and windy environment to ensure long-term stable operation.

    Applications

    Hull segment lifting is the core use of shipyard gantry cranes, large shipyards to build more than 10,000 tons of ships, the need to split the hull into multiple segments for processing, and then through the giant gantry cranes will be lifted to the dry dock, for accurate docking assembly.

    Large offshore structure assembly, such as offshore platforms, ship superstructure lifting, these components are heavy weight, large volume, ordinary cranes can not carry, can only rely on shipyard gantry cranes to complete.

    Ship maintenance operations, when large ships need to be repaired, shipyard gantry cranes can lift the ship’s engine, propulsion system and other heavy parts, to facilitate maintenance personnel to overhaul and replace.

    Henan Mine Crane manufactured Shipbuilding Gantry Crane

    Key Industrial Applications of Cranes

    Manufacturing Industry

    Manufacturing industry is one of the most widely used areas of cranes, throughout the entire process from raw materials to finished products. In the production line, cranes are responsible for handling raw materials, semi-finished products, components, connecting the various processing procedures.

    For example, in automobile manufacturing plants, cranes transport steel, engine, body and other components to the assembly line to ensure the continuity of production; machinery processing plants, cranes carry processed mechanical parts to reduce manual handling errors and labor intensity.

    Construction and Infrastructure

    Construction and infrastructure projects are almost inseparable from cranes. From the foundation construction stage of steel, concrete lifting, to the main structure of the steel structure, prefabricated components installation, and then later equipment into the field, all need to crane cooperation.

    In bridge construction, cranes lift prefabricated girders onto piers for installation; in highway construction, cranes move large paving equipment and roadbed materials; in high-rise buildings, tower cranes are responsible for the transfer of materials at high altitude, which is an important guarantee of construction efficiency.

    Ports and Logistics

    Ports and logistics industry, cranes are the core material transfer equipment. Container terminals, gantry cranes, quay cranes are responsible for container loading and unloading, stacking, connecting ships and land transportation.

    Large logistics centers, cranes are responsible for heavy cargo, large equipment handling and storage, especially outdoor yards, gantry cranes and mobile cranes with, can enhance the efficiency of logistics transfer, reduce the backlog of goods.

    Energy and Power Plants

    In the field of energy and power plants, cranes are mainly used for the installation and maintenance of heavy equipment. Power plant equipment such as turbines, generators, boilers, etc., are heavy and bulky, requiring large cranes for lifting and installation.

    In the new energy field, such as wind power and photovoltaic projects, cranes are responsible for lifting and installing fan blades and photovoltaic modules; in the construction of hydroelectric power plants, cranes are used to carry heavy components such as turbines and generator sets to ensure the smooth progress of the project.

    Mining and Heavy Industry

    In the field of mining and heavy industry, cranes are mainly used for bulk material handling and heavy equipment installation. In mines, cranes are used to handle bulk materials such as ores and coal, and cooperate with transportation equipment to complete material transfer.

    Iron and steel mills, cement factories and other heavy industrial enterprises, cranes are responsible for the entry of raw materials, finished products, as well as heavy equipment maintenance, overhaul, is the production of continuous operation of an important guarantee.

    How to Choose the Right Crane Type

    Selection of cranes, do not blindly pursue large tonnage, high configuration, fit their own conditions of choice, is the most economical and practical. Combined with many years of selection experience, I summarized a few key reference factors for your reference.

    Lifting capacity is the primary consideration, to clarify the maximum weight of the goods to be lifted, plus the weight of the spreader, and at the same time reserve 10% -20% of the safety margin, to avoid overloading operations, to ensure safety.

    Span and lifting height should not be ignored, the span should cover the width of the operating area, the lifting height to meet the demand for lifting height of the goods, but also reserve a certain amount of space to avoid interference with the surrounding structure.

    Mobile demand determines the type of crane, if the operating site is fixed, bridge cranes, jib cranes are more suitable; if you need to move flexibly, mobile cranes, tire gantry cranes are more suitable.

    Indoor or outdoor work, directly affect the selection of crane type. For indoor operation, give priority to bridge cranes and jib cranes; for outdoor operation, gantry cranes and mobile cranes should be selected, while considering wind and corrosion resistance requirements.

    Work level is related to the service life of the crane, high operating frequency, long duration of the scene, to choose high working level equipment; operating frequency of the scene is low, you can choose ordinary working level models, reduce costs.

    Safety and automation requirements, adjusted according to the operational scenarios. For high-risk operation scenarios, choose the equipment with perfect safety configuration; for large-scale projects and high-frequency operations, consider cranes with high degree of automation to enhance operational efficiency.

    Advantages of Using Industrial Cranes

    The reason why industrial cranes can become the core equipment of various industries, the core is that it can solve the heavy lifting problems that can not be accomplished manually, bringing real value.

    Can enhance operational efficiency, manual handling of heavy materials is not only time-consuming and laborious, but also prone to errors, cranes can quickly complete the lifting and transfer of materials, reduce operating time, improve overall production efficiency.

    Reduce manual labor intensity, to avoid the risk of personal injury caused by manual handling, especially heavy material handling, cranes can replace a large number of manual labor, reduce the enterprise’s labor costs and safety risks.

    Enhance operational safety, modern cranes are equipped with comprehensive safety protection devices, such as overload protection, limit protection, emergency braking, can effectively avoid safety accidents in the lifting process, to protect personnel and equipment safety.

    Achieve efficient heavy material handling, for hundreds of tons, thousands of tons of heavy components, only cranes can complete the lifting operation, which is artificial and other small lifting tools can not be replaced, but also industrial production, infrastructure projects to promote the smooth progress of the guarantee.

    Frequently Asked Questions

    Combined with the usual reception of customer experience, I have compiled a few of the most frequently asked questions, answered in an easy-to-understand way, to help you quickly clear up the selection and use of the key questions.

    What are the most common crane types used in industry?

    The most common crane types used in industry, there are four main types: overhead cranes (suitable for indoor workshops), gantry cranes (suitable for outdoor yards), mobile cranes (suitable for temporary work), jib cranes (suitable for fixed work stations). These four models cover most of the industrial lifting scenarios, and are the types that purchasers choose the most.

    What is the difference between gantry cranes and overhead cranes?

    The core difference lies in the support structure and working environment. Gantry cranes have independent legs and do not need to be attached to the plant, so they are suitable for outdoor work; overhead cranes do not have legs and are installed on the plant rail, so they can only work indoors. In addition, gantry cranes have a larger span and a more flexible operating range, while overhead cranes are more suitable for precise indoor operations.

    Which crane is best for outdoor applications?

    Gantry cranes are preferred for outdoor operations, especially rail and tire gantry cranes, which have large span and strong wind resistance, and can cover large operating areas such as open yards and ports. If it is a temporary outdoor work, mobility scene, mobile cranes (such as truck cranes) is more suitable, can be quickly deployed, flexible transfer.

    How do I determine the required crane capacity?

    First calculate the maximum weight of the goods to be lifted, then add the weight of the spreader (such as hooks, grabs), and finally reserve 10% -20% of the safety margin, the sum is the required crane capacity. For example, the maximum cargo weight of 50 tons, spreader weight of 2 tons, reserve 10% margin, choose more than 57 tons of crane can be.

    Can cranes be customized for specific industrial applications?

    Of course, customization is the core feature of industrial cranes. Almost all the core parameters can be customized, such as lifting capacity, span, lifting height, moving mode, but also according to the operating environment can be customized anti-corrosion, wind, explosion-proof and other features, fully adapted to the specific operating scenarios, to solve the special lifting needs.

    Conclusion

    Different types of cranes have their own adaptable scenes, there is no “universal model”. Industrial lifting needs are diverse, from small indoor workshop handling, to outdoor heavy lifting, from the fixed workstation precision work, to the field of temporary work, all need to correspond to the type of crane to complete.

    What Can Henan Mining Crane Factory Offer You?

    If you are selecting cranes for your project, and are not sure which type and which parameters are suitable for your operation scenario, you may want to submit the detailed parameters of your project (lifting capacity, operating site, application industry, etc.), and we will provide you with free technical consultation.

    Henan Mine Crane Factory supply, as a professional crane manufacturer, integrates R&D, design, manufacturing, sales and service to provide customers Please feel free to contact us, we will provide you with free design drawings, and field survey!

    Henan Mine CraneDiscuss your requirements ↗
  • Diesel RTG vs Electric RTG Crane: Which Is More Cost-Effective?

    Diesel RTG vs Electric RTG Crane: Which Is More Cost-Effective?

    Diesel RTG vs Electric RTG Crane: Which Is More Cost-Effective?

    In Henan Mine Crane‘s more than ten years of RTG crane sales and technical service, I have seen too many terminals stepping on the pit in equipment selection. Especially in these years, the global fuel price fluctuation is getting bigger and bigger, the carbon emission regulations of each country’s ports are getting tighter and tighter, almost every customer who comes to consulting, will ask the same question: diesel RTG and electric RTG, in the end, which is more cost-effective?

    Many people’s judgment on this issue only stays on the comparison of equipment purchase price. But people who do port equipment are clear that the service life of RTG can be up to 15-20 years, the cost-effectiveness is never just look at how much money spent when buying, but to look at the more than ten years, the equipment in the end, how much revenue can be brought, and how much expenditure will be incurred.

    Today I will combine Henan Mine Crane’s hands-on experience in serving hundreds of ports around the world, and calculate the account of the two types of equipment from multiple dimensions, such as initial investment, operating costs, full life cycle benefits, and environmental compliance. We don’t talk about false theories, but only talk about the real costs and benefits in the terminal operation, and help you choose the equipment that is really suitable for your terminal.

    What Is a Diesel RTG Crane?

    Definition

    Diesel RTG, also known as tire gantry crane, the core power source is a diesel engine driven generator set. All of its traveling, lifting and trolley running movements are driven by diesel power generation, which is a mature model used in port yards for decades.

    Most of the terminals we have contacted in developing regions have diesel RTGs as their initial equipment, which do not rely on external power grids, and can be used right away, with minimal infrastructure requirements, to quickly meet the needs of terminals in their initial operation.

    Key Characteristics

    Independent power source is the core feature of diesel RTG. It does not require external cables or skid wires, and can move freely throughout the yard without any restrictions on transfer operations, making it ideal for terminals where the yard layout is frequently adjusted or where the operating area is not fixed.

    The lack of a fixed electrical infrastructure means that it has a very low entry threshold. There is no need to build substations, no need to lay slip lines, no need to do cable trench, as long as the yard road surface is up to standard, the equipment can be transported to the site and debugged to start work, which can help terminals to save a lot of time and cost of the preliminary infrastructure.

    Typical Applications

    Medium-sized ports are the most important application scenarios for diesel RTG. These terminals have medium throughput and large fluctuation in operation volume, and the flexibility of diesel RTG can be well adapted to the operation demand at different times.

    There are also terminals in developing regions with limited infrastructure, such as some ports in Southeast Asia and Africa, where the capacity of the power grid is insufficient or the power supply is unstable. The self-powered nature of diesel RTGs allows them to be free from power grid constraints and to stably complete their operations.

    In addition, the old terminals that do not have the supporting slip line system, when expanding or updating the equipment, they will also give priority to the diesel RTG, without having to do a large-scale renovation of the existing yard, it can directly replenish the production capacity of the equipment, and the cost of renovation is very low.

    What Is an Electric RTG Crane?

    rubber tyred gantry crane maneuverability

    rubber tyred gantry crane maneuverability

    Definition

    An electric RTG is a tire-type gantry crane that relies on external grid power. There are three main forms of power sources: cable reel system, skid line system, and safety skid line system.

    Unlike diesel RTG, it does not have a large diesel generator set, the core power comes from the power grid, through different power supply methods, the power is delivered to the driving mechanism of the equipment to complete all the operational actions.

    Henan Mine Crane’s electric RTG program for customers now will match different power supply methods according to the yard layout and operational requirements of the terminal. For example, for fixed block operation, the slip wire solution is more stable; for occasional transfer, the cable reel solution is more flexible.

    Key Characteristics

    Low emission is the most intuitive advantage of electric RTG. It has no diesel engine, so it does not produce exhaust emission directly during operation, and the noise level is much lower than diesel RTG, which can greatly improve the operating environment of the terminal, and it can also fit in the current green development trend of the global ports.

    Zero fuel consumption is the core cost difference between it and diesel RTG. There is no need to purchase diesel fuel, and you only need to pay for electricity, which in the vast majority of the world is much more stable and lower than the cost of diesel fuel, helping terminals to lock in long-term energy expenditures.

    Then there’s the higher efficiency of energy utilization. Diesel engines have an energy conversion rate of only 30-40%, while electric drive systems can achieve an energy conversion rate of 80% or more, and even taking into account grid transmission losses, the overall energy efficiency far exceeds that of diesel models.

    CAPEX Comparison: Initial Investment

    Diesel RTG Capital Cost

    Looking at the purchase price of the equipment itself, the initial investment of a diesel RTG is much lower. Its power system is a mature diesel generator set, the technology threshold is not high, and the manufacturing cost of the whole machine is 15%-20% lower than that of electric RTG.

    More importantly, diesel RTG does not require additional electrical infrastructure investment. There is no need to build a substation, no need to lay slip wire, no need to make cable trench, and no need to do a large-scale remodeling of the yard’s power supply system, which saves a large amount of infrastructure costs.

    For many terminals with limited initial capital, the low-threshold advantage of diesel RTG is very obvious. No need to invest a large amount of money to do infrastructure, just buy the equipment can be put into production, can quickly return to the capital, to ease the early capital pressure.

    Electric RTG Capital Cost

    The purchase price of electric RTG is higher. It requires additional configuration of variable frequency drive system, power supply receiving device, and supporting electrical control system, and the manufacturing cost of the whole machine is higher than that of the diesel model.

    In addition to the equipment itself, electric RTGs require additional infrastructure investment. Regardless of whether it is a slipline or cable reel solution, it requires the construction of a supporting substation, power supply lines, and the electrical infrastructure of the yard. This infrastructure cost, depending on the size of the yard, can be as little as several hundred thousand dollars or as much as tens of millions.

    For a new terminal in China, the purchase price of 12 electric RTGs was nearly two million dollars higher than a diesel model of the same specification. Together with the infrastructure investment for the slip lines and substation, the overall initial investment was nearly ten million dollars higher than a diesel solution.

    Infrastructure Investment Impact

    The layout and construction status of the yard will directly affect the infrastructure cost of electric RTG. The cost advantage of a new terminal is much larger than that of an old one.

    In the planning stage of new terminals, the electric RTG power supply infrastructure can be synchronized into the planning, without the need to do the second transformation of the yard, the cost of civil and electrical construction can be reduced by more than 30%, and will not affect the commissioning of the terminal schedule.

    On the other hand, if an old terminal in operation is to be converted into an electric RTG, it is necessary to do a large-scale reconstruction of the existing yard pavement and power supply system, which is not only costly, but also affects the normal operation of the terminal, and the overall initial investment will be further increased.

    OPEX Comparison: Operating Costs

    Fuel vs Electricity Cost

    Energy cost is the largest fixed expense in RTG operation, and is also the core cost difference between the two models.

    Factor Diesel RTG Electric RTG
    Energy Source Diesel fuel Grid electricity
    Energy Cost Stability Volatile More predictable
    Cost per Move Higher Lower (in most regions)

    We have done a real test, for the same specification RTG, to complete a standard container lifting operation, the diesel model needs to consume 2-2.2 liters of diesel fuel, while the electric model only needs to consume 2-3 kWh of electricity. According to the current oil and electricity prices in most regions of the world, the energy cost of a single operation of the electric model can be about 70% lower than that of the diesel model.

    This cost difference varies from region to region. Europe’s diesel prices are high, the carbon tax is also high, the energy cost advantage of electric RTG is very obvious; the Middle East diesel prices are low, the cost advantage of the electric motor type will be weakened, and more depends on the terminal’s sustainable development strategy; Southeast Asia and part of Africa, the power grid is unstable, the price of electricity fluctuates a lot, and diesel type of cost stability is better.

    There is another important point, diesel price is affected by the international situation, the supply and demand relationship is very big, fluctuations are frequent, it is difficult for the terminal to lock the long-term energy cost; while the fluctuation of the price of electricity is much smaller, the terminal can more accurately do the long-term cost budget.

    Maintenance Cost

    The maintenance cost of diesel RTG is much higher than that of electric RTG. The core reason is that the maintenance workload of diesel engine is extremely high.

    Diesel engines need regular maintenance, every 100 hours or so, we need to do a small maintenance, replace the oil, diesel filter, oil filter, air filter. Every 1,000 hours to do a major maintenance, check the engine block, piston, injector nozzle and other core components, a few years to do an engine overhaul, a single overhaul costs can reach hundreds of thousands of dollars.

    There are also hydraulic systems, cooling system maintenance. Diesel-type cooling system working in a high-temperature environment for a long time, prone to clogging, leakage, need to be regularly cleaned and repaired, but also increase maintenance costs.

    The maintenance workload of electric RTG is much smaller. It does not have a diesel engine, eliminating all engine-related maintenance work, no oil changes, no filter changes, and no engine overhaul.

    The core components of the electric motor type are the motor and the electrical control system, with fewer moving parts, lower wear rate and lower maintenance frequency. Only need to do regular inspection of electrical wiring, lubrication and maintenance of the motor, the average annual maintenance cost can be 30%-50% lower than the diesel engine type.

    Tire Wear

    There is little difference in tire wear between the two models. Tire wear is mainly related to the road conditions in the yard, the operator’s driving habits, and the steering frequency of the equipment, and there is no direct correlation with the form of power.

    However, electric RTGs have smoother acceleration and deceleration control, without the frustration of diesel engines, so operators can control the equipment’s movement and steering more smoothly, which to a certain extent reduces abnormal tire wear and prolongs the service life of tires.

    10-20 Year Lifecycle Cost Analysis

    Total Cost of Ownership (TCO) Model

    To truly determine which of the two models is the better value, a 10-20 year Total Cost of Ownership (TCO) model must be used, and looking at the initial purchase price alone will make a complete misjudgment.

    A complete TCO model must include these parts: initial equipment procurement costs, infrastructure investment costs, 15 years of energy costs, average annual maintenance costs, failure and downtime loss costs, and the residual value of the equipment after use.

    We have done a calculation for a domestic terminal with an annual throughput of 1 million TEUs. For RTGs of the same specification, the initial procurement + infrastructure cost of the diesel model is nearly ten million dollars lower than that of the electric motor model. However, after 15 years of operation, the energy cost and maintenance cost of the diesel model is nearly 40 million higher than that of the electric model, and the whole life cycle cost of the electric model is about 30% lower than that of the diesel model.

    Break-Even Analysis

    Many customers ask how long it will take for an electric RTG to pay for itself with a higher initial investment. This break-even point is mainly affected by two factors: the difference between local diesel and electricity prices, and the annual operating hours of the equipment.

    We have done some calculations, under the domestic oil price and electricity price level, the payback cycle of an electric motor is 3-5 years for an RTG with an annual operating time of 3,000 hours; if the annual operating time can reach 4,000 hours, the payback cycle can be shortened to less than 3 years.

    In Europe, the price of diesel is high and there is carbon tax, the payback cycle of the electric model can be shortened to 2-3 years; while in the Middle East, the price of diesel is low, the payback cycle will be lengthened to 5-7 years, or even longer.

    Simply put, the larger the terminal’s operating capacity, the longer the annual operating hours, and the greater the difference between local oil and electricity prices, the faster the payback of electric RTGs, and the more obvious the long-term cost advantage.

    Environmental & ESG Impact

    Carbon Emission Reduction

    The green transformation of global ports is no longer a trend, but a mandatory requirement, according to the IMO’s Shipping Emission Reduction Report, about 3% of the world’s carbon emissions come from port operations, and diesel RTG are one of the main sources of carbon emissions in ports.

    Diesel RTG will directly emit greenhouse gases and pollutants such as carbon dioxide and nitrogen oxides during operation, and the carbon emission of a diesel RTG in a year can reach several hundred tons. An electric RTG has no direct carbon emissions at the operation site, and even counting the carbon emissions from grid power generation, the overall carbon emissions can be reduced by more than 70%, and if green power is used, near-zero emissions can be realized.

    IMO and Port Environmental Regulations

    Port environmental regulations around the world are getting tighter and tighter, which is at the heart of why many terminals are having to consider electric RTGs.

    The European Union’s Carbon Border Adjustment Mechanism (CBAM), as well as national non-road mobile machinery emission regulations, have imposed strict limits on carbon emissions from port equipment. Ports such as Hong Kong and Singapore have also introduced regulations to limit the use of high-emission diesel equipment in their ports.

    The ports of Los Angeles and Long Beach in the United States have even made it clear that the goal of zero emission from cargo handling equipment will be realized by 2030. In the future, diesel RTGs that do not meet the emission requirements will face the risk of being restricted and forced out of use, and terminals will also have to pay additional taxes related to carbon emissions.

    ESG & Green Port Certification

    Electric RTGs bring not only cost and compliance advantages, but also ESG value. Nowadays, global shipping companies and cargo owners are more and more concerned about the green development capability of ports, and will prefer to cooperate with ports that comply with green standards.

    Terminals with green port certification can not only enhance their brand influence, but also obtain more green financing channels. Many international financial institutions will provide low-interest loans for green port projects, which can help terminals reduce financing costs.

    We have served several terminals in Europe, through the replacement of electric RTGs, to get the green port certification, not only to reduce operating costs, but also to attract more shipping companies to cooperate, throughput has increased significantly.

    Automation and Smart Port Readiness

    Integration with TOS

    Nowadays, ports around the world are developing in the direction of automation and intelligence, and the integration capability of RTG, as the core equipment for yard operation, with the Terminal Operating System (TOS) is becoming more and more important.

    Both models can be integrated with the TOS system, but the electric system is better adapted in the automated terminal. The electric RTG’s drive system is fully electrically controlled, which can be more accurately interfaced with the TOS system and automated dispatching system, with higher control accuracy and faster response time, and is more suitable for automated operations.

    It is difficult to accurately match the engine start/stop and power output of diesel RTGs with automation systems. In automated operation scenarios, there will be problems of untimely power response and increased energy consumption, and the adaptability is far less than that of electric RTGs.

    Energy Management Systems

    Electric RTG can be better connected to the port’s intelligent energy management system to realize finer energy control.

    Through smart grid integration, electric RTGs can adjust the operating power according to the load condition of the power grid, avoiding the peak of electricity consumption and utilizing the low valley tariff to further reduce the energy cost. It can also reasonably distribute the power load of multiple equipment through load balancing to avoid overloading the power grid and ensure stable power supply.

    In addition, electric RTG can be equipped with a regenerative braking system, which converts the kinetic energy generated during the process of container descent and equipment braking into electrical energy and feeds it back into the power grid, further reducing energy consumption. This is something that cannot be achieved with diesel RTGs.

    Future-Ready Infrastructure

    The automation transformation of ports is not a short-term project, but a long-term plan for 10-20 years. By choosing electric RTGs now, we are actually preparing for future automation upgrades.

    Nowadays, almost all newly built automated terminals adopt electric RTG or RMG as the core equipment of the yard. Laying out electric RTG now, when doing automation upgrading in the future, we don’t need to do large-scale remodeling of the power system of the equipment, and we don’t need to supplement the infrastructure investment, which can significantly reduce the cost of upgrading in the future.

    Diesel RTG, almost no space for full automation upgrade. When ports promote automation in the future, diesel equipment will probably be eliminated, and terminals will need to re-invest funds to purchase new electric equipment, which will result in greater waste.

    Regional Cost Comparison

    Middle East Ports

    The Middle East region is characterized by low diesel prices and abundant supply, and the energy cost advantage of electric RTGs has been significantly reduced.

    For most terminals in the Middle East, diesel RTGs are still a very competitive option with low initial investment and low operating costs. But now that countries such as the UAE and Saudi Arabia are promoting the construction of green ports and smart ports, and Saudi Arabia’s Vision 2030 includes a clear carbon reduction target for ports, the use of electric RTGs is gradually increasing.

    In this region, the choice of which model to use depends more on the terminal’s sustainable development strategy than on a mere cost comparison. Terminals with a long-term green development plan will gradually move towards electrification, while terminals with a short-term cost focus will continue to mainstream diesel RTGs.

    Europe

    Europe is the region with the highest penetration of electric RTGs, centered on high fuel costs and strict carbon regulations.

    With the high price of diesel fuel in Europe and the carbon tax, the operating cost of diesel RTG is very high. At the same time, the EU’s environmental regulations on port equipment emissions requirements are extremely strict, the old diesel RTG faces the risk of forced obsolescence.

    In this region, electric RTGs are the preferred choice for almost all new terminals due to their obvious full life cycle cost advantages, short payback period and ability to meet environmental compliance requirements. Maersk Terminals has already completed the electrification of all its RTGs at several of its terminals in Europe.

    Southeast Asia & Africa

    Most ports in Southeast Asia and Africa are characterized by limited infrastructure, insufficient grid capacity and unstable power supply, making the flexibility of diesel RTGs an obvious advantage.

    Many of the terminals in these regions do not have a stable power grid supply, and the stable operation of electric RTGs cannot be guaranteed. At the same time, the throughput of the terminals is generally not high, and the operation volume fluctuates greatly. The low initial investment and high flexibility of diesel RTGs can be better adapted to this scenario.

    However, with the development of ports in these regions, the gradual improvement of power grid infrastructure, coupled with the transmission of global environmental protection requirements, the application of electric RTGs is also gradually increasing, especially in Singapore, Malaysia and other regions with better infrastructure conditions.

    Diesel RTG Advantages

    The core advantage of diesel RTG is the low initial investment and low entry threshold. There is no need to do complex electrical infrastructure, the equipment can be used as soon as it is delivered to the site, which is very suitable for terminals with limited initial capital and insufficient infrastructure conditions.

    It does not rely on the power grid and can operate stably in areas with unstable power supply, which is an advantage that electric RTGs cannot match. In areas with poor grid infrastructure, diesel RTGs are almost the only option.

    It also has high operational flexibility and can be freely transferred throughout the yard without being restricted by cables or skid wires, making it ideal for terminals with an irregular yard layout, frequently adjusted operating areas, or terminals that need to temporarily replenish production capacity.

    Electric RTG Advantages

    The biggest advantage of electric RTGs is their low long-term operating costs. Although the initial investment is high, the energy and maintenance costs are much lower than those of diesel models, and the total life cycle cost advantage is obvious over a 10-20 year life cycle.

    It meets the requirements of increasingly stringent environmental regulations, has no tailpipe emissions and low noise levels, which can help terminals get green port certification, avoid carbon emission-related taxes and compliance risks, and take advantage of the competition in future ports.

    There is also less maintenance work and higher equipment availability. Without the frequent maintenance of diesel engines, there is a lower incidence of breakdowns and less downtime for maintenance, which can be put into operation more often and improve the overall throughput capacity of the terminal.

    Finally, it is better suited for future automated port upgrades, and is now the mainstream choice for new terminals, leaving plenty of room for long-term growth.

    Common Buyer Mistakes

    In the course of serving customers, I have seen too many terminals stepping into the pitfalls when selecting a model, and the most common mistakes almost always lead to a significant increase in costs later.

    The first mistake is to compare only the purchase price of the equipment, ignoring the full life cycle cost. Many terminals only see the diesel RTG buy cheap, directly made the choice, did not count the subsequent more than ten years of fuel and maintenance costs, the results of a few years only to find that the overall expenditure is much higher than the electric model.

    The second mistake is to ignore the impact of infrastructure costs. Some terminals, when planning electric RTGs, only count the price of the equipment but not the infrastructure inputs such as sliding contact lines and substations, and as a result, halfway through the project, they find that the budget has been overspent, and the project schedule has been seriously affected.

    The third mistake is underestimating the fluctuation of fuel prices. Many terminals in the selection, in accordance with the low oil prices at the time to do costing, the results of subsequent oil prices rose sharply, the operating costs of diesel RTG directly doubled, the terminal’s profits were seriously engulfed.

    The fourth mistake, is not calculate the full life cycle cost of 15 years, only look at the short-term expenditure of 3-5 years, ignoring the long-term use of equipment costs. Many marinas use them for 5 years before realizing that the cost of the diesel model has exceeded that of the electric model, but there is no turning back.

    The fifth mistake is to ignore future environmental regulations. Many marinas do not take into account future local emissions regulations when selecting a model, and as a result, within a few years of use, the diesel model does not meet the new emissions requirements, facing mandatory obsolescence, and having to re-invest in replacing the equipment.

    Decision Checklist

    In order to make it easier for you to quickly determine which model is suitable for your terminal, I have compiled a decision checklist, against which you can make a more reasonable choice.

    1. What is the annual operating hours of a single unit? Annual operating hours of more than 3,000 hours, the advantages of electric machine models will be very obvious.
    2. What are the local diesel and electricity prices? The greater the difference between the two prices, the faster the payback of the electric model.
    3. Does the terminal have a clear sustainability strategy and carbon reduction target? If so, electric models are a better choice for long-term planning.
    4. Does the terminal have sufficient grid capacity? Is the power supply stable? If the power grid is not stable, diesel engine is a more stable choice.
    5. Is there any automation upgrade plan for the terminal in the future? If so, electric models are better suited for subsequent upgrades.
    6. Are there any clear requirements on the emission of harbor equipment under local environmental regulations? If there are strict emission restrictions, an electric model will be better suited to meet the compliance requirements.

    Frequently Asked Questions

    Which RTG is cheaper to buy?

    The initial purchase price of a diesel RTG is usually lower. It does not require an additional electrical package, the overall manufacturing cost is 15-20% lower than electric RTGs, and there is no electrical infrastructure to invest in, so the total upfront investment is lower.

    Note, however, that this is only a cost comparison for the initial purchase, not a full life cycle cost comparison.

    Which RTG is cheaper over 15 years?

    In the vast majority of locations, especially high volume terminals, electric RTGs have a lower whole life cost. Although the initial investment is high, the energy and maintenance costs are much lower than for diesel RTGs, and the additional initial investment is usually recovered in 3-7 years, with ongoing operational savings for the rest of the life cycle.

    Only in terminals with very low diesel prices and very low operating volumes will the long-term cost of diesel RTGs be advantageous.

    Can diesel RTG be converted to electric?

    Can diesel RTG be converted to electric? Yes, there are very mature diesel RTG oil-to-electric solutions in the industry. We have done similar conversion for many terminals, removing the original diesel generator set and replacing it with an electric drive system with cable reel or slip line power supply to realize electric operation.

    This transformation program, without replacing the entire equipment, can help terminals save a lot of equipment procurement costs, while meeting the needs of environmental protection and cost reduction, is the mainstream choice for many old terminals to upgrade. The payback period for retrofitting is usually around 3.5-4 years.

    Which is better for green ports?

    Electric RTG is better for green ports. There is no direct exhaust emission during operation, which can significantly reduce the carbon emission of the port. Meanwhile, the noise level is lower, which can improve the operating environment of the terminal, and it is easier to get the green port certification, which can also meet the requirements of IMO and the environmental protection regulations of various countries.

    Nowadays, most of the green port projects around the world will take electric RTG as the first choice of yard equipment.

    How long is the ROI period for electrification?

    The ROI period for electric RTGs is usually 3-7 years, depending on two core factors: the local oil and electricity price differential and the annual operating hours of the equipment.

    The higher the oil/electricity price differential and the longer the annual operating hours, the faster the payback. For example, in the high oil price region of Europe, the payback period can be shortened to 2-3 years; while in the low oil price region of the Middle East, the payback period will be stretched to 5-7 years.

    Henan Mine Crane Factory Custom

    At the end of the day, there is no absolute who is better between diesel RTGs and electric RTGs, only who is more suitable for your terminal.

    Henan Mine Crane has been doing port lifting equipment for more than 20 years, and has provided hundreds of ports around the world with diesel RTG and electric RTG equipment supply and retrofit programs. We will not simply push a certain type of equipment for you, but will do a complete life cycle costing based on your terminal throughput, infrastructure conditions, local oil and electricity prices, and long-term development plans, so as to help you choose a truly suitable program.

    Whether you are a new terminal for equipment planning, or an old terminal for equipment renewal, you can contact our engineering team, we will give you free cost estimates and program planning, to help you avoid the selection of the pit, to achieve long-term revenue maximization.

    Henan Mine CraneDiscuss your requirements ↗
  • Diesel RTG vs Electric RTG Crane in Middle East Ports: Which Is More Cost-Effective?

    Diesel RTG vs Electric RTG Crane in Middle East Ports: Which Is More Cost-Effective?

    Diesel RTG vs Electric RTG Crane in Middle East Ports: Which Is More Cost-Effective?

    In Henan Mine Crane‘s years of RTG crane sales and technical service, I have run through the major ports of Dubai, Jeddah, Doha, and witnessed the transformation of the Gulf ports from traditional operations to global transshipment hubs.

    Nowadays, almost every port operator in the Middle East, when equipment renewal or expansion, will fall into the same knot: choose diesel RTG or electric RTG, after all, the price of diesel here has an advantage all year round, but the sustainable development goals of the countries are constantly tightening.

    Many people make decisions based on the initial purchase price alone, which is actually a misunderstanding. RTG’s service life can reach 15-20 years, in the Middle East’s high temperature, sand and dust environment, the cost-effectiveness is never a short-term comparison of inputs, but to calculate through the full life cycle of more than ten years of accounts.

    Today, I will combine Henan Mine Crane’s practical experience in serving Middle East ports, not playing with false theories, but only talking about real costs, suitability and long-term benefits, to help you clarify the logic of choosing two kinds of equipment in the Middle East scenarios.

    Middle East Port Context: Unique Decision Factors

    Fuel Pricing in Gulf Countries

    The price of diesel fuel in the Middle East has always been the core advantage of diesel RTG. Compared with Europe, where the price is often more than $1 per liter, the price of diesel here is much lower, and the retail price of diesel in Saudi Arabia is even as low as $0.2/liter, and many countries implement government-regulated pricing.

    This pricing model makes the volatility of diesel prices much lower than in Europe, without having to frequently deal with the fluctuations in operating costs caused by soaring oil prices. In the short term, it is true that diesel RTGs have a more controllable and attractive energy bill.

    However, it is important to note that this advantage is only in the short term. As global pressure to reduce carbon emissions intensifies and countries in the Middle East gradually adjust their energy policies, the price advantage of diesel is likely to diminish in the long term.

    Electricity Pricing Structure

    The difference in industrial electricity price among Middle East countries is not small, the industrial electricity price in Saudi Arabia is between 0.053-0.08 USD/kWh, and the electricity price in UAE, Qatar and other countries are also different, which is mainly determined by the energy policy and power supply structure of each country.

    More noteworthy is that Saudi Arabia, the United Arab Emirates and other countries are increasing investment in renewable energy. Saudi Arabia’s “City of the Future” NEOM’s Oksargon Port, plans to rely entirely on solar, wind and other renewable energy supply, the UAE’s Khalifa Port is also in the layout of the solar power supply system.

    This means that the cost of electricity for electric RTGs in the future has a lot of room to fall. Once connected to the renewable energy grid, the long-term energy cost advantage of electric RTGs will be more obvious, and they will be better suited to the trend of regional energy diversification.

    High-Temperature Operating Environment (45-55°C)

    With summer temperatures in the Middle East often exceeding 45°C, and in extreme cases reaching 55°C, this environment is a huge test for RTG operation, and both diesel and electric models need to be adapted.

    For diesel RTGs, high temperatures put great pressure on the engine. Long-term operation of the engine in a high-temperature environment will accelerate the wear and tear of components, and even overheating and shutdown, greatly affecting the continuity of operations.

    The cooling load of electric RTGs will increase dramatically. Electrical components are easy to deteriorate and short-circuit under high temperature, requiring additional cooling system to maintain normal operation, which will also indirectly increase the energy consumption and maintenance workload a little.

    It can be said that no matter which form of power is chosen for RTGs in Middle East ports, desert heat adaptation is an essential part of the process, which is also a key factor affecting the life of the equipment and operating costs.

    Sand & Dust Conditions

    Middle East ports are generally faced with sand and dust, which is more insidious and long-lasting to RTGs than high temperatures. In many ports, neglecting to protect against sand and dust has led to frequent equipment failures and high maintenance costs.

    For diesel RTGs, sand and dust will frequently block the air filter, which needs to be replaced frequently, otherwise it will lead to insufficient engine air intake, power loss, and even wear out generator parts, shortening the service life of the engine.

    The core danger of electric RTG is in the electrical control cabinet. If sand enters the control cabinet, it will lead to poor contact and short circuit of the electrical components. Therefore, the sealing performance of the electrical cabinet is crucial, and it must reach a high IP protection level in order to resist the intrusion of sand and dust.

    CAPEX Comparison Under Gulf Conditions

    Diesel RTG Capital Investment

    Based on the equipment purchase price alone, the initial investment for a diesel RTG is indeed lower. Diesel RTGs with the same specifications are 15-25% less expensive than electric RTGs, which is attractive to ports with limited capital budgets.

    More critically, diesel RTGs do not require additional investment in yard electrification infrastructure. There is no need to build a substation, lay slip lines or make cable trenches; the equipment is delivered to the site, commissioned and ready to go.

    This is particularly important for many ports in the Middle East that are expanding rapidly. Some medium-sized ports, for example, need to replenish yard capacity quickly, and diesel RTGs can be deployed quickly to meet capacity expansion needs without having to wait for lengthy infrastructure work.

    It is also suitable for temporary or flexible yard layouts, such as short-term leased yards and temporary transfer points, without the need to invest in fixed infrastructure, and with the flexibility to transfer the equipment at the end of the project, thus minimizing investment risk.

    Electric RTG Capital Investment

    The initial investment of electric RTG is much higher, which includes not only the equipment itself, but also a whole set of supporting electrification infrastructure.

    Firstly, the purchase price of the equipment, electric RTG needs to be equipped with variable frequency drive system, power supply receiving device, etc., the cost of the whole machine is higher than the diesel model. Secondly, there is the infrastructure investment, including substation construction, laying of slip wire or cable reel system, yard trenching and cable protection.

    The infrastructure cost will be higher especially when retrofitting an existing operating terminal (brownfield project). It is necessary to remodel the existing yard pavement and operation area, but also to avoid affecting the normal operation, the construction difficulty and cost will be greatly increased.

    Henan Mine Crane once did electric RTG retrofit for an existing terminal in the United Arab Emirates, and only the infrastructure investment of substation and slip wire accounted for more than 30% of the whole project cost, which is the core reason why many old terminals are hesitant to electrify.

    OPEX Comparison in the Middle East

    Fuel Cost vs Electricity Cost

    Diesel fuel is indeed cheaper in the Middle East, which makes the short-term energy cost of diesel RTGs look more advantageous, but the situation is different when it comes to high-utilization terminal scenarios.

    We have done a real test, for the same size RTG, to complete one TEU lifting operation, the diesel model needs to consume 2-2.2 liters of diesel, while the electric model only needs to consume 2-3 kWh of electricity. According to the diesel and electricity price in Saudi Arabia, the energy cost of single operation of electric RTG is 30%-50% lower than that of diesel model.

    Especially in high throughput hubs such as Dubai, Jeddah and Khalifa ports, where the annual operating hours of RTGs can reach more than 4,000 hours, this cost difference will be magnified infinitely. Over the course of a year, an electric RTG can save hundreds of thousands of dollars in energy expenses.

    And while diesel prices are less volatile than in Europe, they are still at risk of rising in the long term, while electricity prices are relatively stable, especially with the spread of renewable energy, and the energy costs of electric RTGs will be more manageable.

    Maintenance Cost in Desert Climate

    In the hot and dusty environment of the Middle East, the difference in maintenance cost between the two types of RTGs is very obvious, and this is the biggest headache for many ports in the later stages.

    The maintenance of diesel RTGs focuses on the engine. The high temperature will accelerate the engine wear, need to do frequent maintenance, every 100 hours or so to change the oil, filter, every 1,000 hours to do a major maintenance, a few years but also to do an engine overhaul, a single overhaul costs can reach hundreds of thousands of dollars.

    Sand and dust will also increase the maintenance workload, air filters, fuel filters need to be replaced often, otherwise it will lead to engine failure. For one of our Saudi customers, the filter replacement frequency for diesel RTGs is more than double that of temperate regions.

    An electric RTG is much simpler to maintain. It does not have a diesel engine, eliminating all engine-related maintenance, no oil changes, no injector repairs, and maintenance focuses on the electrical and cooling systems.

    Although the electrical and cooling systems of electric RTGs need to be checked regularly, the overall maintenance frequency and cost is 30%-50% lower than that of diesel RTGs, which can save a lot of money in the long run.

    Equipment Availability Rate

    For high throughput transshipment hubs in the Middle East, the equipment availability rate of RTGs has a direct impact on the efficiency of the port’s throughput, and a minute of downtime can be costly.

    Electric RTGs typically have a higher availability rate. It has fewer mechanical parts and fewer points of failure, especially since there are no diesel engines that are prone to problems, and engine-related downtime is virtually non-existent.

    Diesel RTGs, on the other hand, are often down due to engine overheating, clogged filters, worn components, and other issues, and the rate of downtime rises significantly, especially during the hot summer months.

    For example, at Dubai’s Jebel Ali Port, after replacing electric RTGs, equipment availability increased from 88% to more than 95%, reducing congestion and losses caused by downtime, which is one of the core reasons why many large hub ports tend to choose electric RTGs.

    15-20 Year Lifecycle Cost Modeling (Gulf Scenario)

    Key Variables in ROI Model

    To truly determine which is more cost-effective, diesel RTGs or electric RTGs, it is necessary to establish a 15-20 year Total Lifecycle Cost (TCO) model, in which there are several key variables that directly determine the return on investment for both types of equipment.

    The first is the annual hours of operation. In large transshipment hubs in the UAE and Saudi Arabia, the annual operating hours of RTGs are generally over 4,000-5,000 hours, and the larger the operating volume, the more obvious the cost advantage of electric RTGs; if it is a small or medium-sized port, with less than 3,000 operating hours per year, the short-term advantage of diesel RTGs will be more prominent.

    Secondly, there is the risk of fuel price escalation. Although the Middle East diesel prices are low now, but in the long run, with the carbon emission reduction policy to promote, diesel prices may rise, while the price of electricity will decline with the popularization of renewable energy, which will further widen the cost gap between the two.

    There are also maintenance cycles in high-temperature environments, and trends in carbon regulations. Environmental regulations are tightening in the Middle East, and in the future diesel RTGs may have to pay a carbon tax, which will also increase long-term operating costs.

    Break-Even Analysis (Typical Gulf Scenario)

    Many Middle East port customers ask how long it will take for electric RTGs to pay back the high initial investment. Based on our experience in the Middle East, the break-even point depends on the annual operating hours of the RTG.

    If the annual operating hours of RTGs are above 4,000-5,000 hours, the payback period of electric RTGs is usually 4-7 years under the electricity and diesel price levels in Saudi Arabia and the UAE.

    The higher the operating volume, the faster the payback. For example, in Abu Dhabi’s Khalifa Port, where RTGs operate more than 5,000 hours a year, the payback cycle for electric RTGs took just over four years, with significant savings in operating costs every subsequent year.

    However, for small and medium-sized ports with less than 3,000 hours of operation per year, the payback period can stretch to 7-10 years or more, in which case the short-term economics of diesel RTGs are more favorable.

    ESG, Sustainability & Vision 2030 Impact

    Saudi Vision 2030

    Saudi Arabia’s “Vision 2030” sets out clear requirements for the sustainability and intelligent transformation of ports, which is a core factor that must be taken into account when selecting RTGs for Saudi ports.

    This is also the core factor that must be considered when choosing RTGs for Saudi ports. The vision clearly puts forward the need to build smart ports and green logistics corridors, get rid of dependence on oil, and promote economic diversification. And electric RTGs, as low-emission and environmentally friendly equipment, are an important support for realizing this goal.

    Saudi Arabia spent $500 billion to build the Port of Oksargon, as the “City of the Future” NEOM core component, it is planned to use fully automated, renewable energy-driven equipment, electric RTG has become the preferred model of the port, the future will also realize the whole process of automated operations.

    For Saudi ports, the choice of electric RTGs is not only a cost consideration, but also an inevitable choice in line with the national strategy to obtain more policy support and resources.

    UAE Green Port Initiatives

    The UAE Green Port Initiatives are more forward-looking than Saudi Arabia’s, especially the ports in Dubai and Abu Dhabi, which are already promoting electrification on a large scale.

    Dubai Ports World (DP World) has a clear sustainability roadmap with the goal of achieving carbon neutrality in port operations, and electric RTGs are a key piece of equipment to achieve this. Khalifa Port, the UAE’s core port, has deployed 20 electric RTGs and has also built a solar-powered system to further reduce carbon emissions.

    What’s more, green port projects in the UAE can be supported by green financing. Many international financial institutions offer low-interest loans to ports that adopt environmentally friendly equipment, which can significantly reduce port financing costs.

    ESG Financing Advantage

    With ESG concepts now commonplace around the world, electric RTGs can bring significant financing advantages to Middle East ports that are unmatched by diesel RTGs.

    Electric RTGs can significantly reduce a port’s Scope 1 emissions, improve its ESG rating, and attract more international investors. At the same time, ports equipped with electric RTGs are more likely to qualify for green bond issuance and broaden financing channels.

    The high emissions of diesel RTGs, on the other hand, will expose ports to long-term regulatory risks. In the future, if the Middle East countries introduce stricter carbon emission regulations, diesel RTGs may be restricted or even phased out, bringing additional losses to ports.

    Grid Stability & Infrastructure Challenges

    Grid Capacity in Industrial Zones

    The normal operation of electric RTGs cannot be achieved without stable grid support, which is also a key consideration for Middle East ports when choosing electric RTGs.

    In major industrial hubs such as Dubai, Abu Dhabi and Jeddah, there is sufficient grid capacity and stable power supply to meet the demand of electric RTGs without worrying about grid overload.

    However, in some remote ports with limited grid capacity and less stable power supply, large-scale deployment of electric RTGs will face grid pressure. In this case, if electric RTGs are chosen hastily, there may be insufficient power supply and the equipment may not be able to operate normally.

    Substation Investment Planning

    Substation construction is a significant investment in electric RTG infrastructure, and requires advance planning to reduce long-term costs.

    If it is a new port (greenfield project), planning the electric RTG substation and power supply line in the planning stage can significantly reduce the infrastructure cost and avoid the trouble of later renovation.

    When we made a plan for a new port in the Middle East, we synchronized the construction of the substation with the overall port infrastructure, which saved 25% of the cost and shortened the commissioning cycle of the project compared with the additional construction later.

    For the renovation of existing terminals, the construction of substations needs to take into account the compatibility of the existing site and power supply lines, which makes the construction more difficult and costly, so detailed planning and calculations need to be done in advance.

    Hybrid Transition Strategy

    For many Middle Eastern ports, the transition from diesel RTG to pure electric RTG is not only costly, but may also face challenges in terms of power grid and technology. A diesel-electric hybrid RTG is a good transition option.

    Hybrid RTG combines the advantages of diesel and electric, which can be powered by diesel when the grid is insufficient and switch to electric mode when the grid is stable, reducing energy costs and emissions.

    Moreover, hybrid RTGs can be upgraded to pure electric RTGs at a later stage without having to replace the entire equipment, only the power system needs to be modified, which can help ports save a lot of equipment replacement costs. This transition strategy is ideal for ports that have long-term electrification plans, but short-term capital or infrastructure shortfalls.

    Desert Climate Engineering Considerations

    Hisilicon K3

    Diesel RTG Adaptation

    The desert climate of the Middle East places high demands on diesel RTG adaptations, and equipment that is not properly adapted will have a much higher failure rate and a shorter service life.

    First of all, the cooling system must be equipped with a heavy-duty cooling system to increase the radiator area and improve the cooling efficiency in order to prevent the engine from overheating and shutting down under high temperature. For the diesel RTGs we give to our Middle East customers, the cooling systems are customized to adapt to the extreme high temperatures of 55℃.

    Next is the engine oil, which must be selected as a high-temperature special oil, which can maintain good lubrication performance in high-temperature environments and reduce the wear and tear of engine parts.

    The filtration system should also be strengthened by adopting multi-stage air filtration and frequent replacement of filters to prevent sand and dust from entering the engine, thus avoiding engine wear and malfunction.

    Electric RTG Adaptation

    The desert adaptation of electric RTG focuses on the protection of the electrical system, the core of which is to resist high temperature and sand and dust.

    The electrical control cabinet must be equipped with an air conditioning system to keep the temperature inside the cabinet stable and prevent the electrical components from aging and short-circuiting under high temperature. At the same time, the use of heat-resistant insulating materials to enhance the high-temperature resistance of the electrical system, as in the case of the ultra-high-temperature sand and dust units designed for the Middle East environment, to ensure that key components operate reliably at high temperatures.

    The sealing performance of the electrical cabinet is also crucial, and it must be designed with IP67 and above grade sealing to create sand-proof IP-rated enclosures to prevent sand and dust from entering and protect the electrical components.

    In addition, cables must also be protected, using high-temperature-resistant, anti-abrasion cables to avoid aging and breakage caused by sand, dust and high temperatures.

    Strategic Decision Matrix for Gulf Ports

    Scenario Recommended Option
    Rapid yard expansion Diesel RTG
    High-volume transshipment hub Electric RTG
    Vision 2030 alignment Electric RTG
    Remote port with limited grid Diesel RTG
    Long-term ESG financing strategy Electric RTG

    This decision matrix, which is summarized from our practical experience with dozens of ports in the Middle East, can help you quickly match your own scenario. The core logic is: diesel for short-term expansion, electric for long-term development; diesel for remote ports, electric for core hubs.

    Common Mistakes in Gulf Projects

    These years of service in the Middle East ports, I have seen a lot of projects because of selection errors, resulting in a substantial increase in the cost of late, summarized, there are several common mistakes, we must avoid.

    The first mistake, just because the diesel fuel is cheap, blindly choose diesel RTG, ignoring the long-term ESG pressure and maintenance costs, many ports with 5-6 years, because of the tightening of environmental regulations and maintenance costs are too high, have to replace the electric RTG, but increased investment.

    The second mistake, underestimated the impact of high temperature on the engine. Many ports use conventional diesel RTGs without high-temperature adaptation, resulting in frequent engine overheating and shutdown in summer, seriously affecting operational efficiency, and later additional transformation costs.

    The third mistake is that there is no planning for electrification infrastructure when building new ports. Many new ports try to save trouble by deploying diesel RTGs first, and when they want to upgrade electric RTGs later, they find that there are no locations reserved for slip lines and substations in the yard, which makes it extremely difficult to transform, and the cost has doubled several times.

    The fourth mistake is that they only compare the unit price of the equipment and ignore the TCO at the system level. many ports only look at the cheapness of diesel RTGs when they buy them, but they do not calculate the fuel and maintenance costs for more than ten years or the long-term energy-saving benefits of electric RTGs, and then make the wrong decision.

    Decision Checklist for Middle East Port Operators

    In order to facilitate your quick decision-making, I have organized a simple checklist, against which you can avoid most of the selection pits.

    1. What is the annual operating hours of RTGs in your port? If it is more than 4000 hours, give priority to electric RTG.

    2. What are the local diesel price and industrial electricity price? The greater the difference between the two prices, the more obvious the advantage of electric RTG.

    3. Does your port have sustainability goals that are aligned with Saudi Vision 2030, UAE Green Ports Initiative? If so, electric RTGs are more appropriate.

    4. Do you have a 15+ year plan for port expansion? Electric RTGs are more cost stable in the long run.

    5. is green financing important to your port? Electric RTG can help you get more green financing support.

    6. Is your yard a new construction or a retrofit of an existing yard? New yards are prioritized for electric RTG infrastructure, while existing yards may consider a hybrid transition.

    Frequently Asked Questions (Middle East Focus)

    Is diesel still cheaper in Gulf countries?

    In the short term, yes. The price of diesel in the Middle East is regulated by the government and is cheaper than in many parts of Europe and Asia, so short-term operating costs are indeed lower.

    But in the long run, the cost advantage will gradually shrink. While the price of diesel is likely to rise in line with carbon policies, the cost of electricity for electric RTGs will fall as renewable energy becomes more widely available, and electric RTGs have lower maintenance costs, making them more advantageous in terms of whole life costs.

    Is electric RTG practical in 50°C?

    Yes, as long as it is properly adapted to the desert. The electric RTGs we have supplied to our customers in Dubai and Saudi Arabia have been retrofitted for high temperature and dust resistance.

    Equipped with air-conditioned electrical control cabinets, heat-resistant insulation and sand-proof seals, and optimized cooling systems, electric RTGs are able to operate stably at extreme temperatures of up to 55°C, with an equipment availability rate of more than 95%, which is the same as that of diesel RTGs.

    How long is the ROI in Saudi or UAE ports?

    It mainly depends on the annual operating hours of the RTG. In the high throughput ports of Saudi Arabia and UAE, the annual operating hours of RTGs are more than 4,000 hours, and the payback period of electric RTGs is usually 4-7 years.

    The higher the operational capacity, the faster the payback. For example, Khalifa Port’s electric RTGs, which operate over 5,000 hours per year, recouped the additional initial investment in just over four years, with significant annual operating cost savings to follow.

    Can diesel RTGs be retrofitted later?

    Can diesel RTGs be retrofitted later? Yes, and there are very mature retrofitting programs now, just like Konecranes’ skid line retrofitting program, and Henan Mine Crane has also done oil-to-electricity and hybrid retrofitting of diesel RTGs for many Middle East ports.

    By removing the diesel genset and adding an electric drive system and power receiving devices (such as skid lines and cable reels), diesel RTGs can be converted to hybrid or electric RTGs without replacing the whole equipment, which can save a lot of investment.

    Which option aligns better with Vision 2030?

    There is no doubt that an electric or hybrid RTG system is the way to go. Saudi Arabia’s Vision 2030 is centered on sustainable development and smart ports, and electric RTGs, with their low emissions and environmentally friendly features, are perfectly suited to this goal.

    Electric RTGs have become the centerpiece of smart ports in Saudi Arabia, as in the case of the Port of Oksargon, and choosing electric or hybrid RTGs will also allow the port to receive more policy support and resources.

    Conclusion

    Back to the original question: which is more cost-effective for Middle East ports, diesel RTG or electric RTG? In fact, there is no absolute answer, the core depends on your port scenario and long-term planning.

    The advantages of diesel RTG are clear: low initial investment, fast deployment, no dependence on the grid, suitable for rapid expansion, remote ports, or small and medium-sized ports with short-term financial constraints. Its short-term economics are outstanding, but it will face high maintenance costs and environmental compliance risks in the long term.

    Electric RTGs have high initial investment and infrastructure requirements, but the long-term advantages are clear: low energy and maintenance costs, environmental compliance, adaptability to smart port transformation, and access to green financing. Especially in high throughput hubs like Dubai and Jeddah, the full life cycle cost advantages of electric RTGs will become increasingly obvious.

    Henan Mine Crane Factory Custom

    Henan Mine Crane has been doing port lifting equipment for more than 20 years, and has provided equipment supply and transformation programs for diesel RTGs and electric RTGs to dozens of ports in the Middle East, so it is familiar with the Middle East’s climate, policies, and port operation characteristics.

    We will not simply push a certain type of equipment for you, but according to your port throughput, annual operating hours, local oil and electricity prices, long-term planning, to give you a complete life cycle costing, to help you choose a truly suitable program.

    Whether you are a new port to do equipment planning, or old ports to do equipment renewal, renovation, you can contact our engineering team, we will give you free cost estimates and program planning, to help you avoid the selection of the pit, to achieve long-term revenue maximization.

    Henan Mine CraneDiscuss your requirements ↗