Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

作者: YUWEI, YUWEI

  • How to Choose an Overhead Crane for Your Workshop? (Complete Buyer’s Guide)

    How to Choose an Overhead Crane for Your Workshop? (Complete Buyer’s Guide)

    How to Choose an Overhead Crane for Your Workshop? (Complete Buyer’s Guide)

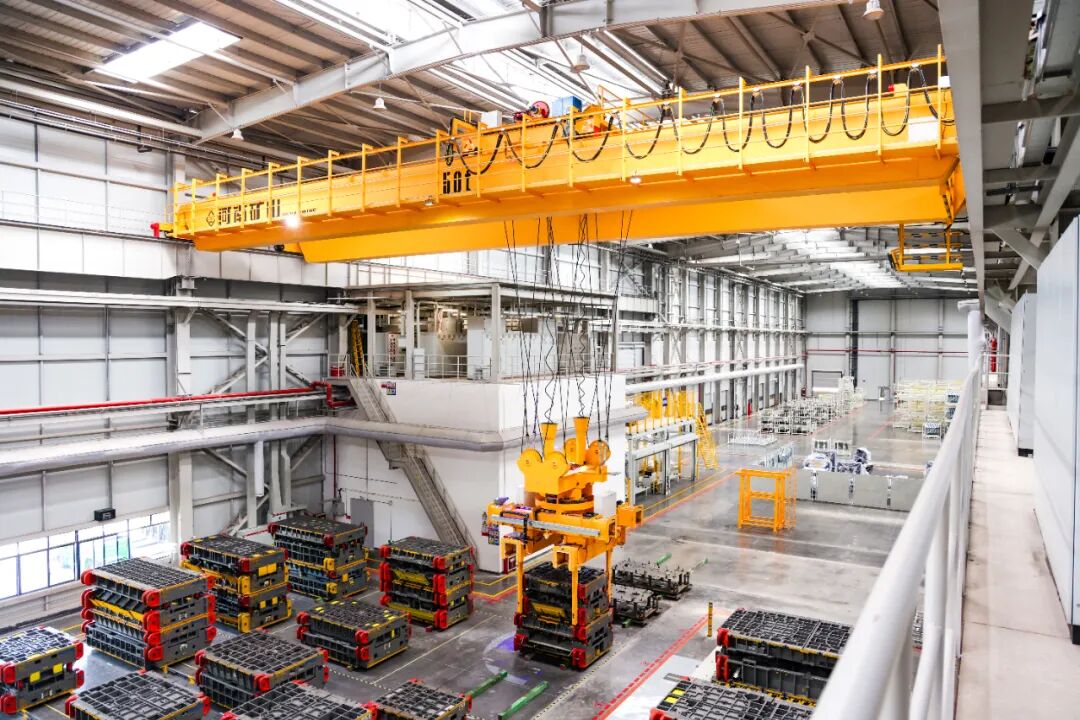
    Overhead cranes are the workhorses of the workshop, whether it’s moving raw materials, assembling machine tools or transferring finished products. Choose a suitable workshop overhead crane, can save a lot of things; but if you choose the wrong, trouble will ensue.

    I do in Henan Mine Crane workshop crane sales and technical support for almost ten years, I have seen too many customers stepping on the pit: some cheap to buy the load is not enough equipment, just use half a year on the failure; some did not calculate the workshop span, half of the area after the installation of cranes can not be hoisted; there are also ignored the working environment, in the high temperature workshop with ordinary cranes, less than a year on the aging of the components.

    Today combined with my years of front-line experience, step by step to teach you to choose the right workshop overhead crane.  whether you are a small processing plant, standard manufacturing plant, or heavy industrial plant, read this can find the right model for you.
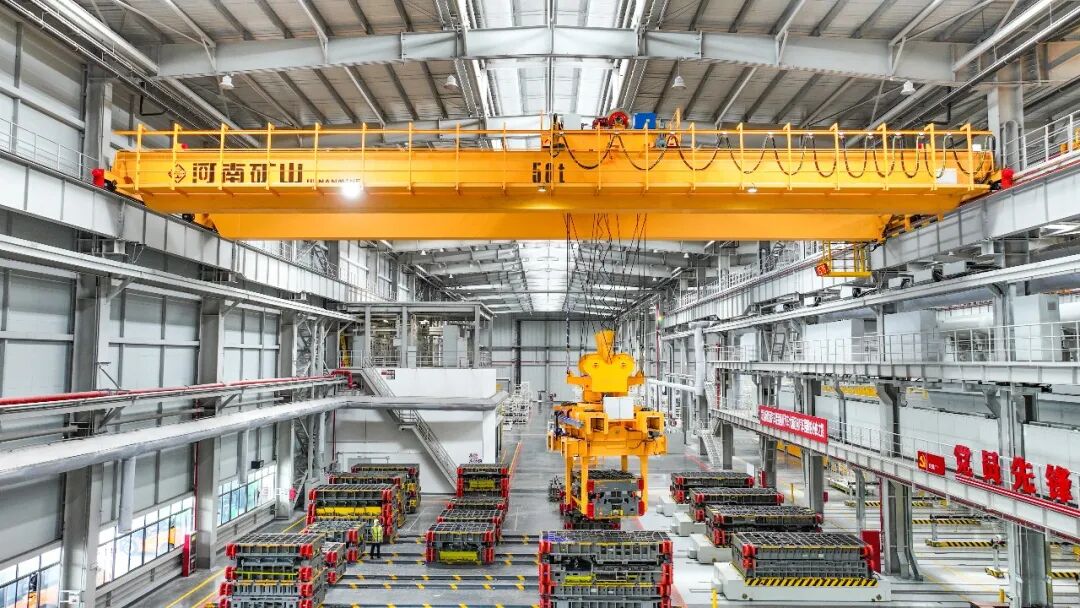
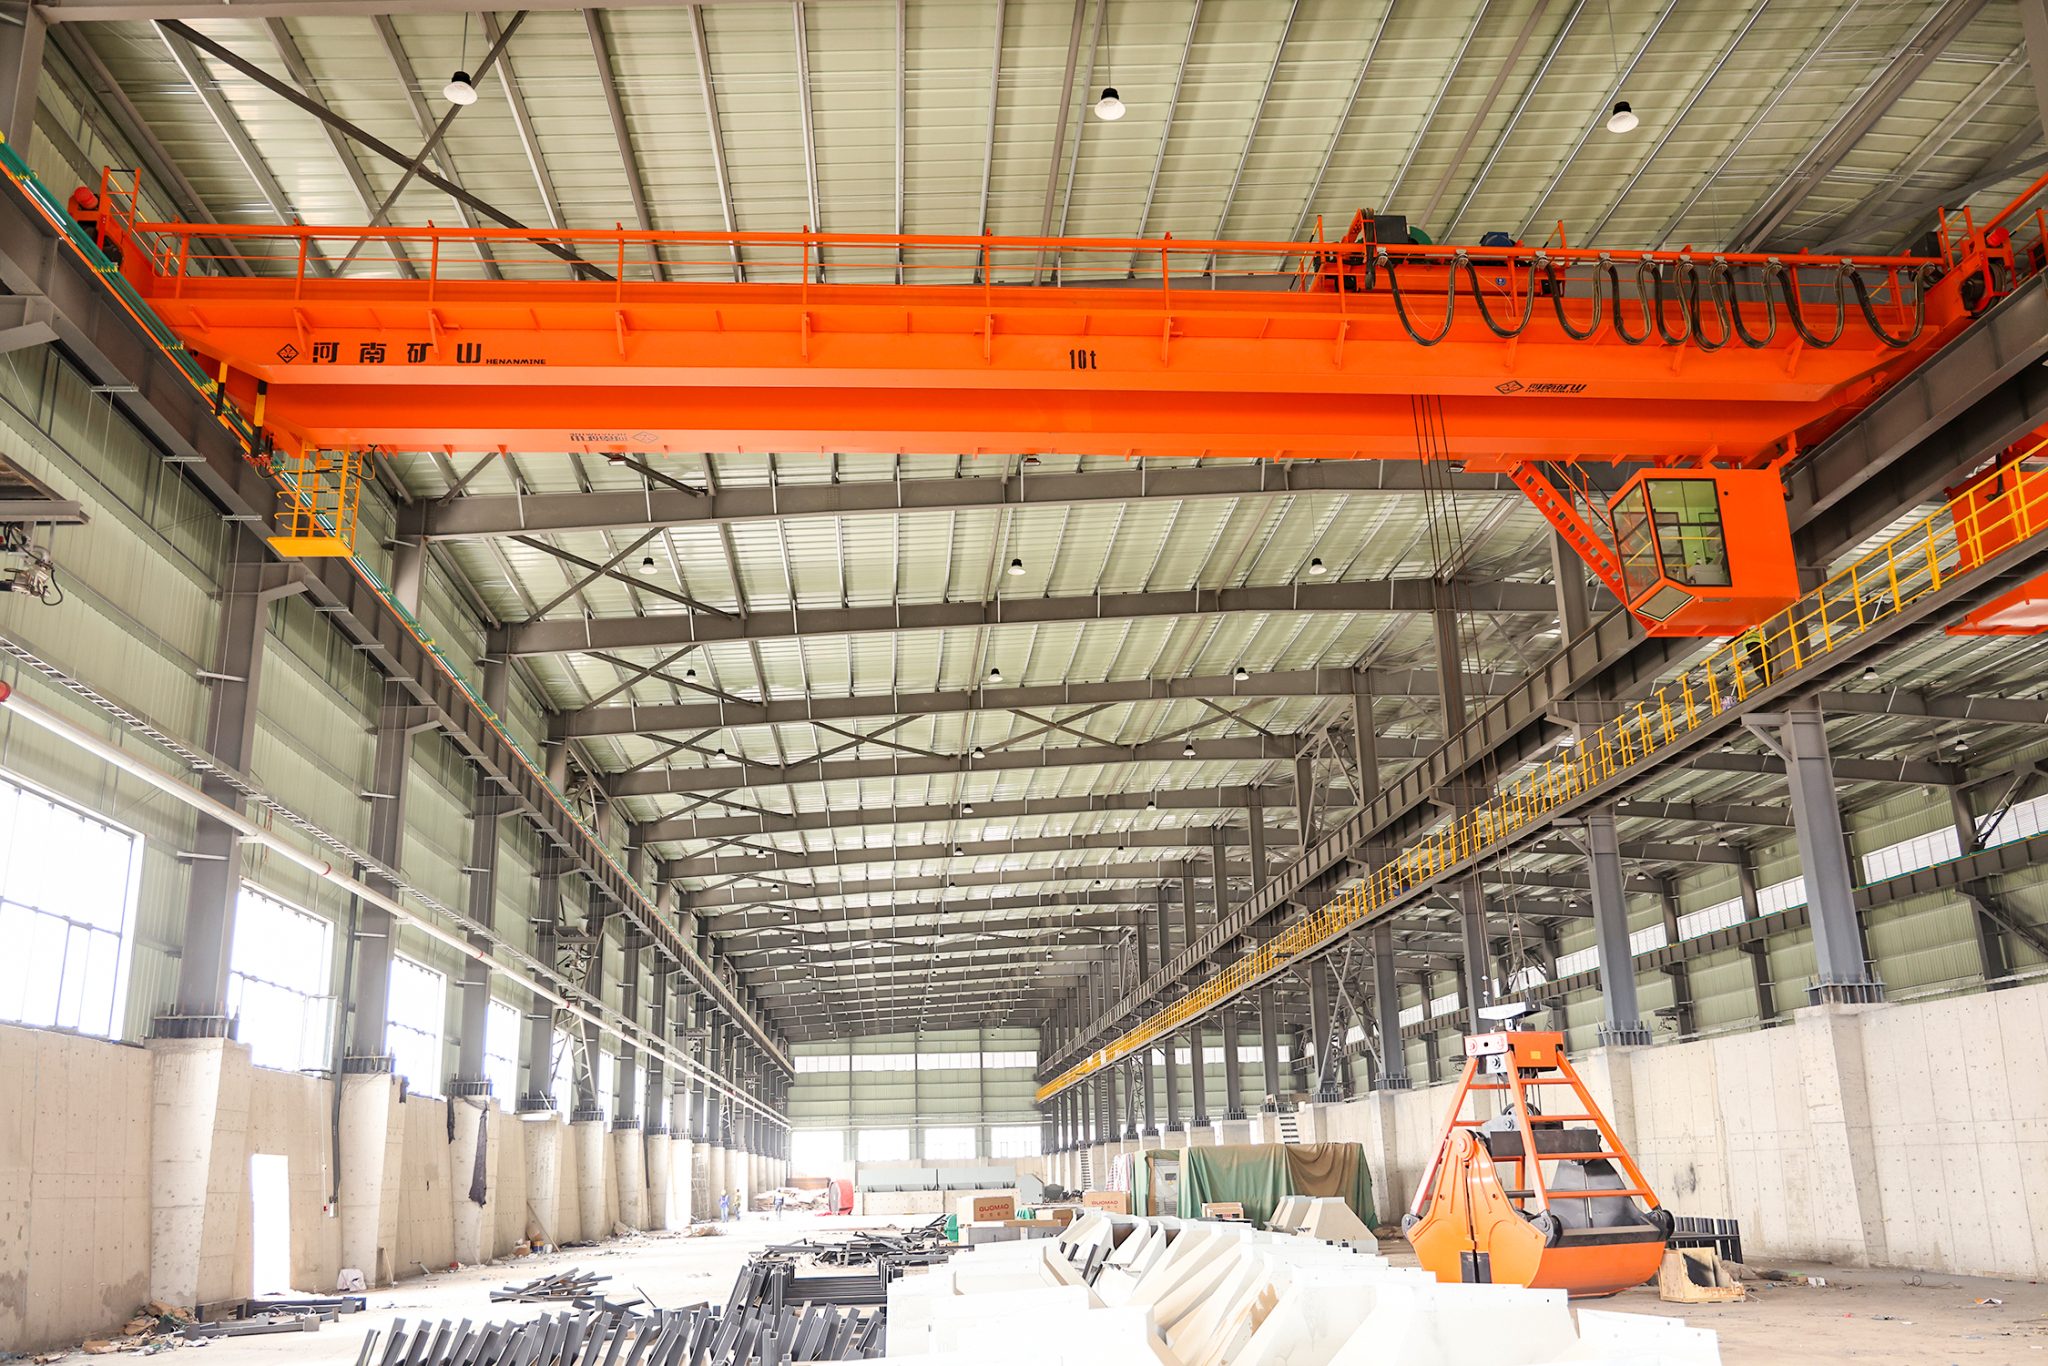
    overhead crane for workshop Henan Mine Crane Factory supply

     Define Your Lifting Needs

    1. Load capacity

    When choosing a crane, the first step is to calculate your maximum lifting weight, which is called rated lifting capacity (SWL) in the industry. This step can not be estimated to come, the difference may be a problem.

    1-5 tons of cranes, suitable for light workshops, such as small hardware factories, electronic processing plants, usually mainly hanging some small parts, tools or light raw materials, enough and economical.

    5-20 tons is the most commonly used range, most standard manufacturing workshop, such as machining, automotive parts production, with this tonnage crane is enough, both lifting machine tool parts, but also the transfer of semi-finished products, the most adaptable.

    Above 20 tons belongs to heavy duty cranes, specifically for heavy industrial workshops, such as metallurgical plants, large machinery manufacturing plants, used to hoist heavy machine tools, large castings and forgings, the structure and stability of the equipment requires more.

    Here is a practical advice: no matter how much you calculate the maximum load, leave 10-20% more safety margin.

    2. Span and coverage

    Crane span, to put it simply is the width of your workshop, it directly determines the crane can cover the operating area. The common range of workshop span is from 5 meters to more than 30 meters, and the span demand is different for different sizes of workshops.

    Small workshop span is generally 5-10 meters, choose the corresponding span of the crane on the line; medium-sized workshop span of 10-20 meters, according to the actual width of the workshop needs to be accurately matched; large and heavy workshop, the span can reach 20-30 meters or even larger, you have to choose a large span of special cranes.

    Choose a small span, there will be operational blind spots, such as the workshop on both sides of the material can not be lifted, only frequent movement of materials, both time-consuming and labor intensive; choose a large span, the cost of equipment will increase, and the stability of the operation will be reduced, but also a waste of space in the workshop.

    3. Lifting height

    Lifting height is easy to be ignored, but it directly affects whether the operation can be carried out normally. It depends on two factors: the ceiling height of the workshop, and the equipment clearance required for the operation.

    If your workshop needs to lift large machine tools, tall semi-finished products, the lifting height must be enough to set aside the maximum height of the material plus the height of the spreader, but also to leave at least 500mm of safety clearance, to avoid collision with the ceiling or other equipment when lifting.

    For example, in the machinery assembly workshop, it is often necessary to lift tall machine parts, the lifting height should be at least 8 meters or more; if it is only lifting small parts, the lifting height of 5-8 meters is enough.

    Another point to note, if there are beams and pipes on the ceiling of the workshop, the height of these obstacles should also be deducted to ensure that the crane’s hook can be lifted and lowered properly without being interfered with.

    4. Load Characteristics

    Different workshop lifting loads, shape, weight distribution are different, which will directly affect the configuration of the crane, can not be generalized.

    Some loads are irregular, such as large castings, shaped parts, the center of gravity is not stable, which requires the crane to have a more accurate positioning ability, but also with a special spreader, to prevent shaking when lifting; some loads are very long, such as steel, pipe, the need for cranes to crane more reasonably designed lifting point, to avoid tilting of the load.

    There are also more fragile loads, such as precision instruments, fragile parts, lifting needs to be smooth, can not have violent shaking, which requires cranes equipped with frequency conversion speed control system, to achieve smooth start and stop.
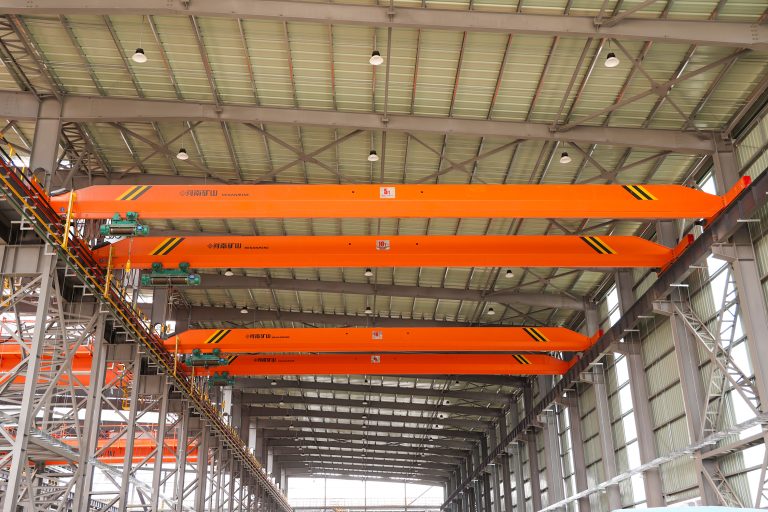
    overhead crane for workshop Henan Mine Crane Factory supply

    Evaluate your workshop structure

    Workshop building structure

    The building structure of the workshop directly determines which kind of crane can be installed. At present, the workshop on the market is mainly divided into two kinds of steel structure and concrete structure, and the adaptability of the two varies greatly.

    The roof of a steel structure workshop has a stronger load-bearing capacity, which is suitable for the installation of overhead cranes running on top without additional reinforcement of the roof, and it is easier to install and simple to maintain in the later stage. Most of the new standard workshops, which are of steel structure, have the best suitability.

    Concrete structure workshop roof load-bearing is relatively weak, before installing the crane, you must first account for the load-bearing capacity of the roof to see if it can support the weight of the crane track beam. If the load bearing is not enough, you can not install the top running crane, you have to choose the self-supporting crane system.

    Self-supporting crane with its own support structure, do not have to rely on the roof of the workshop, directly fixed to the ground, will not damage the original building structure, is the first choice for concrete workshop, old workshop. Our Henan Mine Crane’s self-supporting workshop cranes are fully bolted, with a short installation cycle, no welding, and do not affect the normal production of the workshop.

    Space and clearance limitations

    In addition to the building structure, the space and clearance of the workshop is also very important, which directly affects the design and installation of the crane. Many customers just ignore this point, resulting in the crane can not be used normally after installation.

    First of all, we should consider the ceiling height of the workshop, which directly determines the lifting height of the crane; secondly, the column spacing, the column is too dense will affect the crane’s span selection, you need to adjust the track layout to avoid interference with the column; there are also obstacles in the workshop such as pipelines, lighting equipment, ventilation systems and other obstacles, but also to reserve a safe clearance for the operation of the crane.

    Generally speaking, between the crane and the workshop columns, pipes, ceilings, at least 500mm safety gap should be reserved to prevent collision during operation. If the workshop space is relatively small, we can recommend smaller, lightweight cranes to maximize the use of workshop space.

    New Workshop vs Existing Workshop

    New workshop and existing machine shop, the selection of ideas are completely different, this point must be clear.

    The advantage of the new workshop is that it can be planned in advance, we can cooperate with construction engineers, the crane track, support structure into the workshop design, to avoid the trouble of later remodeling. And the new workshop has no existing structural constraints, according to the lifting needs, free to choose the type of crane and configuration, but also optimize the use of space, reduce installation costs.

    The same is not true for the existing machine shop, which needs to be adapted to the existing building structure and cannot damage the original facilities. In this case, the suspended (under running) crane is a good choice, it is installed under the roof, without taking up additional ground space, and the lower requirements for the roof load-bearing, the installation cycle is short, without having to stop work to transform, many of the existing locomotive room upgrades will choose this model.

    Henan Mine Crane has a wealth of experience in the transformation of the existing locomotive room, we will first conduct a comprehensive survey of the workshop structure, and then according to the actual situation, recommend the most appropriate type of crane, to ensure that the installation does not affect the normal production of the workshop.

     Choose the right type of crane

    1. Single girder overhead crane

    Single girder overhead crane is the most common model in the workshop, with high cost performance, suitable for light to medium load scenarios with load ≤ 20 tons, and the first choice for most workshops.

    It has simple structure, light weight, low load-bearing requirements on the roof of the workshop, short installation period, usually 3-7 days to install and commissioning is completed, and the maintenance is also convenient, no need to specialize in maintenance personnel.

    Small processing plants, electronic factories, small mechanical workshop, choose single girder overhead crane is enough, both to meet the lifting needs, but also to control costs. Our Henan Mine Crane single girder workshop cranes are made of Q345B high-strength steel, which has a more stable structure, and can be customized according to the size of the workshop in terms of span and lifting height, which is suitable for different scenarios.

    In addition, single girder cranes run with low noise, which will not affect the production environment of the workshop, and is suitable for workshops with noise requirements, such as electronic workshops and precision machining workshops.

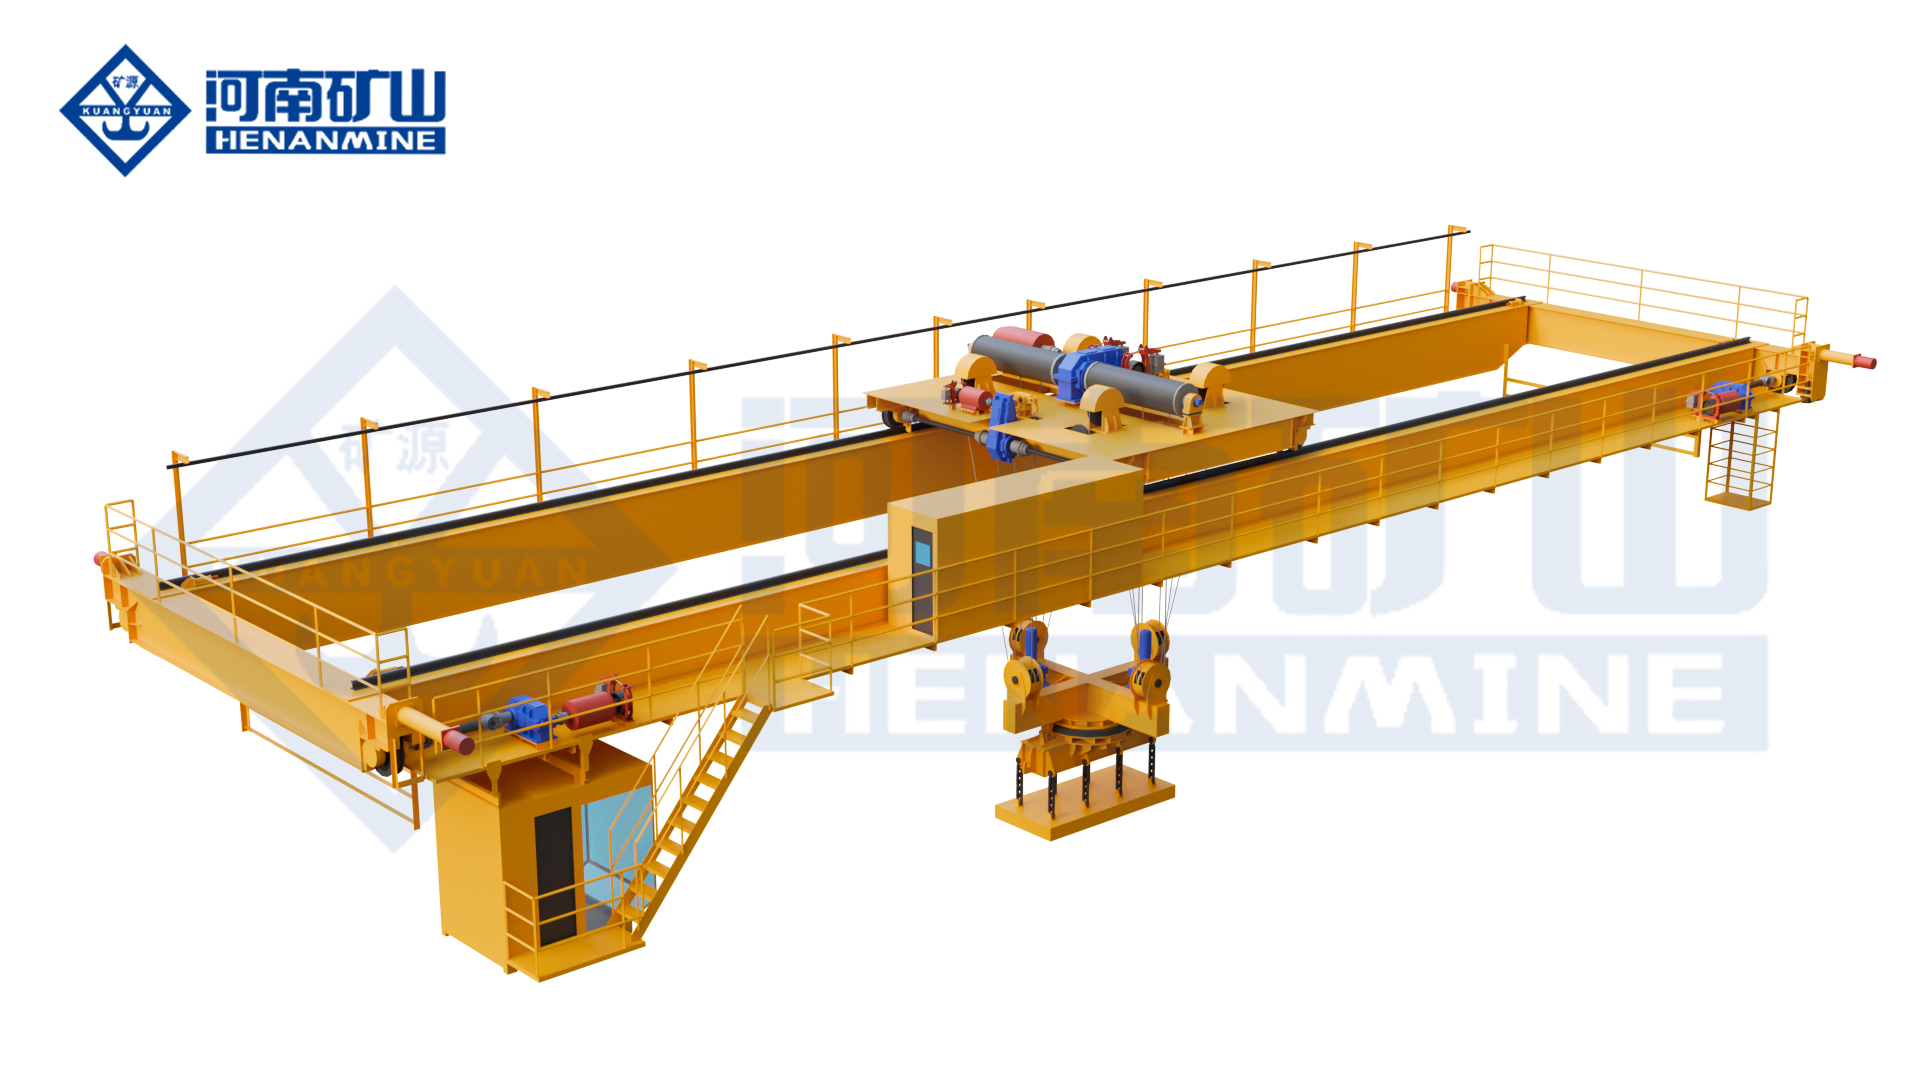
    2. Double Girder Overhead Crane

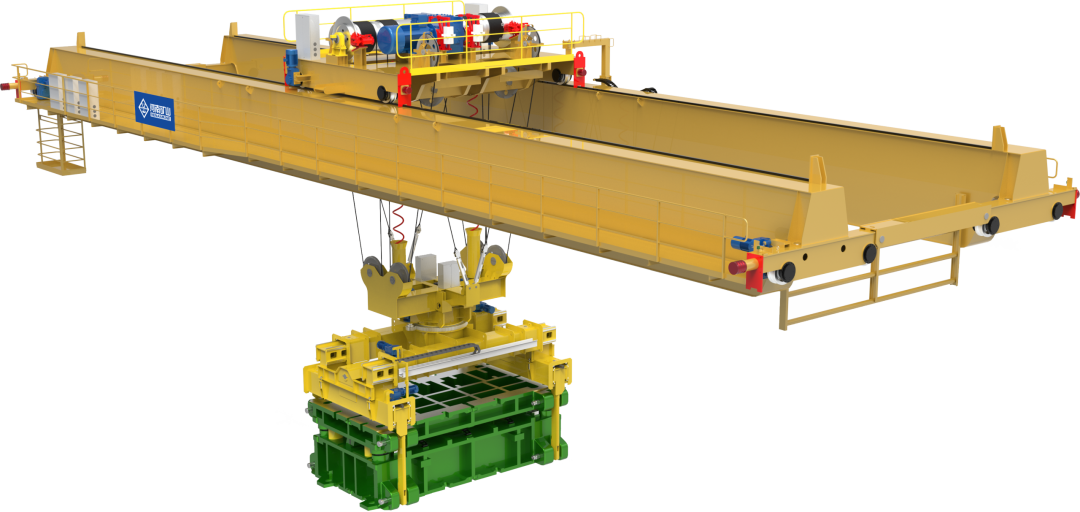
    Double girder overhead crane, mainly used for heavy load, continuous operation of the workshop, such as metallurgical plants, large-scale machinery manufacturing plants, heavy parts processing plants, the load is usually more than 20 tons.

    Its advantages are higher lifting height, better stability, ability to withstand large load operation for a long time, and higher positioning accuracy, suitable for lifting heavy machine tools, large castings and forgings, heavy semi-finished products and so on. The design of double girder structure can also reserve more working space to avoid interference with workshop equipment.

    Although the initial cost of double girder cranes is higher than that of single girder, the stability and durability of the later stage is more guaranteed for workshops that require long-term continuous operation. For example, in metallurgical workshops, where high-temperature steel needs to be lifted continuously every day, the high-temperature-resistant performance and load-bearing capacity of double girder cranes can effectively minimize failures and reduce downtime costs.

    .

    3. Top running vs suspended

    Whether it is a single girder or double girder crane, there are two types of operation: top running (top running) and suspended (under running), both of which have different adaptability scenarios, so choose according to need.

    Top running crane is the most common way of operation, the track is installed on the top of the roof of the workshop, higher carrying capacity, stable operation, easy maintenance, and can realize the whole workshop coverage, suitable for new large-scale workshop, heavy-duty scenarios. Most heavy industrial workshops, will choose the top running crane.

    Suspension cranes, rail mounted below the roof of the workshop, also known as underslung cranes, suitable for low headroom workshop, or existing locomotive room remodeling. It does not take up ground space, and the roof load-bearing requirements are lower, the installation is more flexible, without destroying the original structure.

    Simply put, for new large workshops and heavy load demand, choose top running; for existing locomotive rooms and low headroom scenarios, choose suspended.
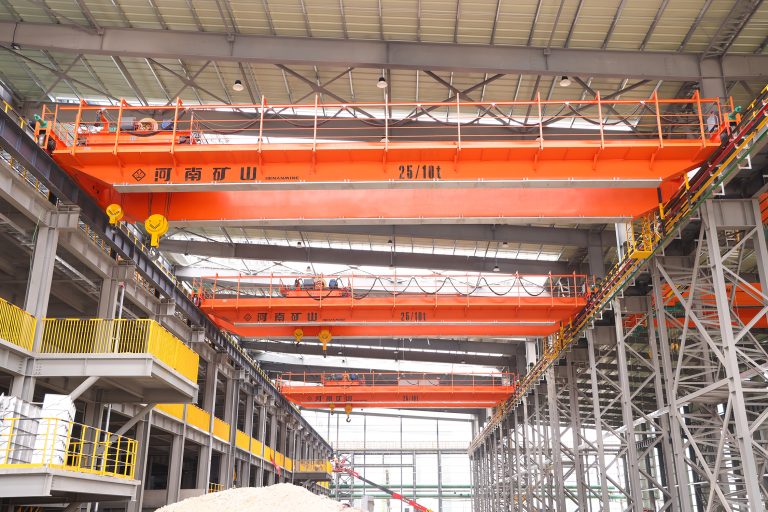
    overhead crane for workshop Henan Mine Crane Factory supply

     Determine the working level

    Classification of working level (ISO / FEM / CMAA)

    Many customers choose cranes, only look at the load and span, ignoring the working level, which is one of the easiest potholes to step on. The working level determines the durability and service life of the crane, and if you don’t choose the right one, the equipment will be easily damaged in advance.

    Workshop crane working level, mainly follow the ISO, FEM, CMAA three international standards, from light to heavy is divided into different levels. Different standards have different grade correspondences, such as FEM’s 1Bm corresponds to CMAA’s Class A, FEM’s 2m corresponds to CMAA’s Class C. Our Henan Mine Crane engineers will help you accurately match to ensure that the equipment meets your frequency of use needs.

    For light load use, such as small workshop, which is used for less than 1 hour per day and lifting materials occasionally, class A3/M3 is enough; for medium frequency use, such as standard manufacturing workshop, which operates for 3-6 hours per day, class A4-A5 is chosen; for heavy workshop with continuous operation, which operates for more than 8 hours per day, you need to choose class A6-A8.

    The working level is mainly determined by the load spectrum and the average daily operating equivalent time, for example, a workshop crane load spectrum for the intermediate level, the average daily operating equivalent time of 1.6 hours, corresponding to the working level of the ISO M5 class, equivalent to the FEM 2m class, we will recommend the appropriate models and configurations based on this data.

    Frequency of use and model recommendation

    Frequency of use directly determines the working level and model selection, do not blindly pursue a high level, nor can you choose too low a level of equipment, otherwise it will affect the service life.

    Occasional use, such as a few times a month, choose a single girder overhead crane, working class A3-A4, low cost, but also to meet the demand; daily use, such as daily production of material transfer, choose a medium working class (A4-A5) single girder or double girder crane, taking into account the cost and durability.

    Continuous use, such as assembly line type production workshop, continuous operation for more than 8 hours a day, you must choose heavy duty double girder cranes, working class A6-A8. In this scenario, the stability and durability of the equipment is more important than the cost, which can effectively reduce failures and avoid downtime affecting production.

    Henan Mine Crane will accurately match the working level according to the usage frequency of your workshop, which will not waste the investment but also ensure the long-term stable operation of the equipment.
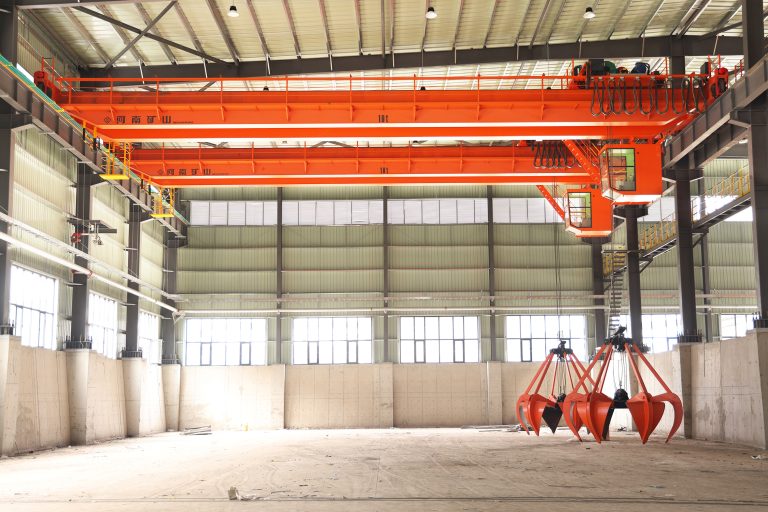
    overhead crane for workshop Henan Mine Crane Factory supply

    Selection of Key Components and Configurations

    Hoist selection

    Hoist is the core component of the crane, equivalent to the “heart” of the crane, which directly affects the stability and safety of lifting, the workshop scene mainly choose two kinds of hoists: wire rope hoists and chain hoists.

    Wire rope hoist is suitable for heavy-duty scenarios, such as lifting heavy machine tools, large parts, strong carrying capacity, high lifting height, and smooth operation, wear-resistant, corrosion-resistant, suitable for long-term use. Our Henan Mine Crane workshop cranes are equipped with high quality wire rope hoists by default, which can be adapted to the working conditions of different workshops.

    Chain hoist is suitable for light load scenarios, such as small workshops, auxiliary lifting, simple structure, easy to operate, and lower cost, and small size, does not take up too much space, suitable for small space workshop.

    In addition, the quality of the hoist is very important, poor quality hoists are prone to broken rope, rope jamming and other faults, there are security risks. Our Henan Mine Crane hoist, after strict quality testing, long service life, and sufficient spare parts, the later replacement is convenient.

    Control system

    Workshop crane control system, there are mainly three kinds, each with adaptable scenes, do not blindly pursue complex, suitable for their own is the best.

    Push-button control (pendant control) is the most basic, low-cost, simple operation, suitable for small workshops, simple lifting operations, such as small hardware factories, usually only lifting small parts and components, with the button control is enough. But its control line length is limited, the operator’s moving range is restricted, not suitable for complex lifting scenes.

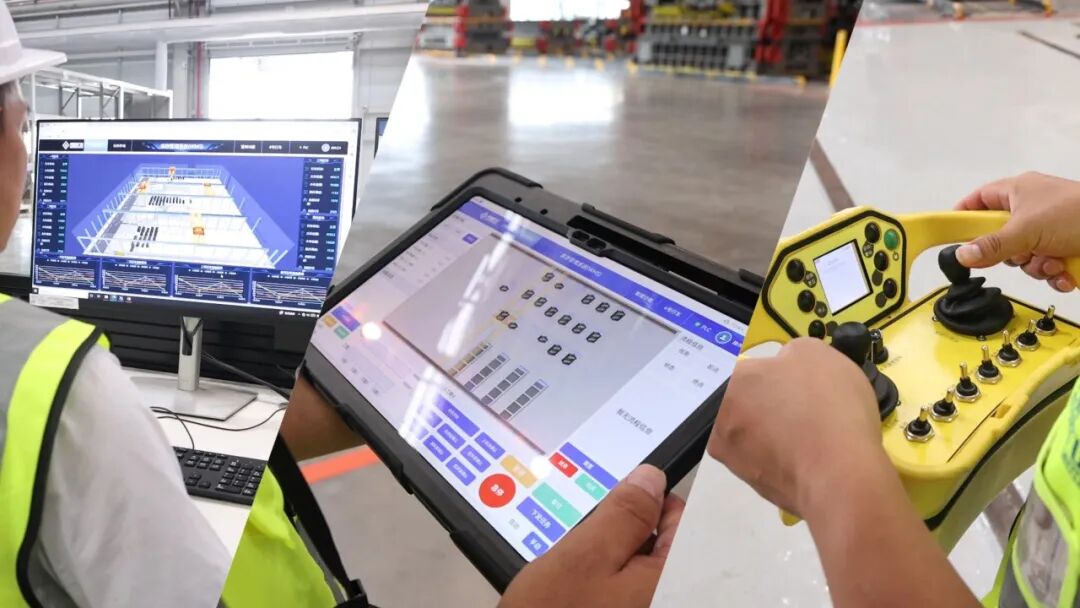
    Remote control is the recommended choice for workshops, and it is also the most mainstream control method at present. The operator can take the remote control, observe the load and the surrounding environment in the best position, move flexibly, and also support multi-person collaboration, and there are multiple safety protections to avoid misuse.

    Henan Mine Crane’s workshop cranes, most of them are equipped with remote control, operating distance is far, signal is stable, and there is an anti-touch design, even if accidentally pressed the wrong button, it will not start the equipment, so the safety is higher.

    Cabin control (cabin control) is seldom used in the workshop scene, only super-large heavy-duty workshops, which require long-term continuous operation, need to be equipped. It has high cost, complicated installation, and limited vision, not as flexible as remote control, generally not recommended for workshop use.

    Speed control system

    The speed control system directly affects the lifting precision, and different workshop scenes have different requirements for speed control.

    Single-speed speed control is low cost, simple operation, suitable for simple lifting operations, such as handling raw materials, finished products, not high precision requirements, single-speed speed control is enough. However, it is not smooth enough to start and stop, easy to cause load shaking, not suitable for lifting fragile, precision parts.

    Variable-frequency speed control (VFD) is the first choice for workshops, especially for scenarios that require lifting precision, such as precision machining workshops and mechanical assembly workshops. It can realize smooth start and stop to avoid load shaking, and it can control the speed finely to realize millimeter-level positioning, which is essential for lifting precision parts, machine tool assembly and other operations.

    Although the cost of frequency conversion speed control is 15-20% higher than single speed, it can effectively protect materials and equipment, reduce safety hazards, and is more cost-effective for long-term use. Henan Mine Crane’s workshop cranes can be equipped with variable frequency speed control system according to customer’s needs to meet the precision requirements of different scenarios.
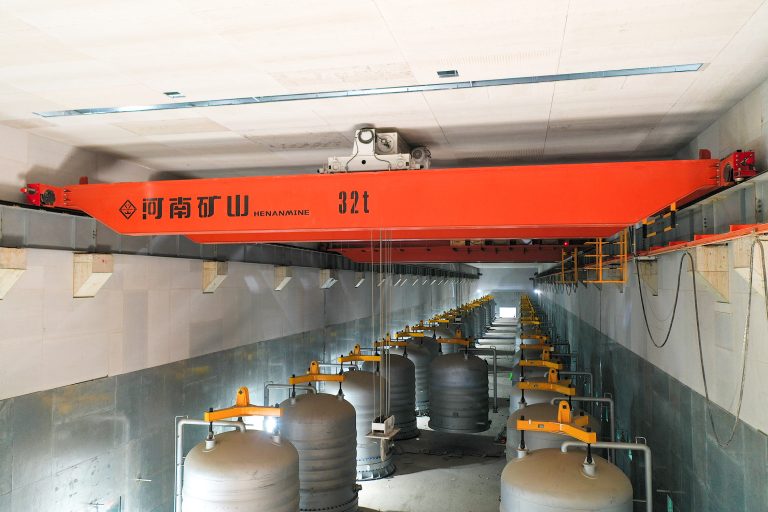
    overhead crane for workshop Henan Mine Crane Factory supply

     Safety and Compliance Standards

    Necessary safety devices

    Workshop operation, safety first. Crane safety devices are indispensable, which are directly related to the safety of operators and equipment, and can also avoid the loss of downtime due to failure.

    Overload protection is necessary to prevent the crane from carrying more than the rated load, to avoid equipment damage and safety accidents; limit switches, including lifting height limit and running stroke limit, can prevent the crane from exceeding the operating range, collision to the workshop equipment or walls.

    Emergency stop button is also very critical, in any position can quickly stop the equipment, to deal with unexpected situations, such as load shaking, equipment failure, can be stopped in a timely manner; Anti-collision system, can detect the distance between the crane or with the obstacles, automatic deceleration or stop, to avoid collision.

    Henan Mine Crane’s workshop cranes, all safety devices comply with international standards, and will be regularly tested to ensure the safety of equipment operation. In addition, we will also add additional safety protection devices according to customer needs, such as windproof device, rainproof device, adapted to different workshop environments.

    International Standard Requirements

    No matter which country you are in, no matter which type of workshop you have, cranes must meet the corresponding international standards, and compliance is a prerequisite. Workshop cranes mainly follow the ISO, FEM, CMAA three major international standards, of which ISO is the global standard, FEM is the European standard, CMAA is the U.S. standard.

    If your workshop is located in the European region, you need to comply with the FEM standard; located in the U.S. region, you need to comply with the CMAA standard; if it is a multinational operation of the enterprise, it is recommended to choose the equipment that meets the globally applicable ISO standard, to avoid compliance problems.

    Henan Mine Crane’s workshop cranes, all products have passed ISO, CE, SGS certification, comply with international standards such as FEM, CMAA, etc. They are exported to many countries and regions, including Russia, Pakistan, Congo, etc., which can meet the compliance requirements of different regions around the world, so you don’t have to worry about compliance issues.
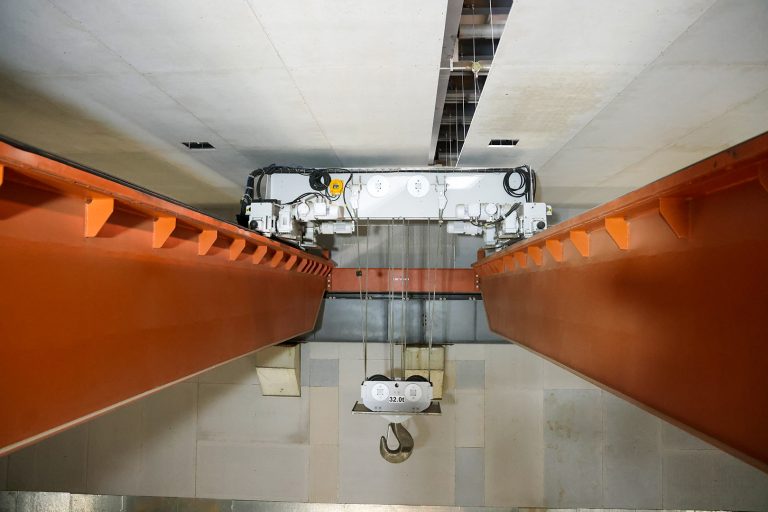
    overhead crane for workshop Henan Mine Crane Factory supply

     Environmental Considerations

    Special Environment Adaptation

    Different workshop environments have different requirements for cranes, especially for special environments, which must be targeted selection, otherwise the equipment will be easily damaged, affecting the service life, but also increase maintenance costs.

    High-temperature environments, such as metallurgical workshop, foundry, high temperature, high loss of crane parts, need to use metallurgical special cranes, equipped with high-temperature resistant parts, good heat insulation to avoid motor, hoist damage due to high temperature. Our Henan Mine Crane metallurgical workshop cranes can work stably under the environment of -40℃ to 80℃, which is suitable for extreme high temperature or high cold scenes.

    Workshops with explosion risk, such as chemical workshop and paint workshop, need to use explosion-proof cranes, the electrical system adopts explosion-proof design to avoid sparks triggering explosions, and all the components should comply with explosion-proof standards to ensure the safety of operation.

    Dusty, high humidity environment, such as mining workshops, workshops in coastal areas, you need to seal the crane motor, electrical cabinet, good dust, moisture, corrosion measures. We Henan Mine Crane will use triple anti-corrosion process, effectively extend the life of the equipment to adapt to the high dust, high humidity environment.

    Environmental impact on cost

    Special environment will increase the design and manufacturing costs of cranes, such as explosion-proof cranes cost about 30% more than ordinary cranes, high temperature, anti-corrosion treatment will also increase the cost, but this part of the investment is necessary.

    If the environmental factors are ignored and ordinary cranes are chosen, the maintenance frequency of the equipment will be greatly increased in special environments, the service life will be shortened, and the maintenance cost and downtime cost in the later period will be much higher than the initial investment. For example, the workshop in coastal areas, do not do anti-corrosion treatment, the crane may be 3-5 years on the rust and corrosion, and do a good job of anti-corrosion treatment, can be used for more than 10 years.

    Henan Mine Crane will recommend the right model and treatment program according to your workshop environment, and try to control the cost while ensuring the adaptability of the equipment, so that you can get a higher cost-effective.

     Life cycle cost (not just initial price)

    Cost Composition (CAPEX + OPEX)

    Many customers choose cranes and only look at the initial purchase price, which is the most common misconception. The total cost of the crane, including the initial investment (CAPEX) and operating costs (OPEX) two parts, can not just focus on the initial price, to calculate the long-term account.

    Initial investment includes the price of the equipment itself, transportation costs, installation and commissioning fees, which is the most intuitive part; operating costs including routine maintenance fees, energy consumption, spare parts replacement, labor costs, etc. This part of the cost is easy to be ignored, but in the long run, the proportion is not low.

    Why cheap is not necessarily good

    Workshop downtime costs are very high, especially the production-oriented workshop, a piece of equipment stopped for a day, the loss may be up to tens of thousands of dollars. The poor quality crane, although the initial price is cheap, but the quality is not reliable, easy to frequent failures, resulting in downtime, this part of the loss is much higher than the difference in the price of the crane.

    Our Henan Mine Crane, although the initial investment is a little higher than the small manufacturers, but the quality of the equipment is reliable, the use of high-quality components, low maintenance frequency, spare parts global supply, can be quickly replaced to reduce downtime. And our equipment has lower energy consumption, long-term use, energy costs can also save a lot.

    For example, a mechanical processing customers, before the selection of a cheap single girder crane, annual maintenance fee of more than 20,000, but also frequent downtime; later replaced with our Henan Mine Crane equipment, annual maintenance fee of less than 10,000, and almost no downtime, two years to recover the difference in price.

    Therefore, the selection of cranes, do not just look at the initial price, to comprehensively consider the full life cycle costs, choose cost-effective, reliable quality equipment, is the most cost-effective.

     Common mistakes to avoid when selecting cranes

    Combined with these years of experience, I summarized a few customers are most likely to step on the pit, we must avoid when selecting the type, you can take a lot less detours.

    Only look at the price, ignoring the quality and after-sales. Many customers figure cheap, buy the equipment of small manufacturers, later failure, can not find after-sales, can only spend their own money to repair, and downtime losses. We Henan Mine Crane has a global after-sales team, no matter which country you are in, we can provide timely maintenance services.

    Neglecting the working level, light-loaded workshop chooses low-level equipment, or heavy-loaded workshop chooses high-level equipment, which will either be damaged in advance or waste the investment. The working level must be selected in combination with the frequency of use, and accurate matching is the best.

    Blind selection without checking the structure of the workshop leads to the crane can not be installed, or need to dismantle the building, increasing costs. Before installation, you must first survey the workshop structure, check the load bearing, and then select the model.

    Underestimation of the lifting height, resulting in the crane and the workshop ceiling, equipment interference, can not work properly; do not take into account the future expansion, such as the later increase in lifting load, expanding the size of the workshop, the equipment can not be adapted to the workshop, can only be replaced.
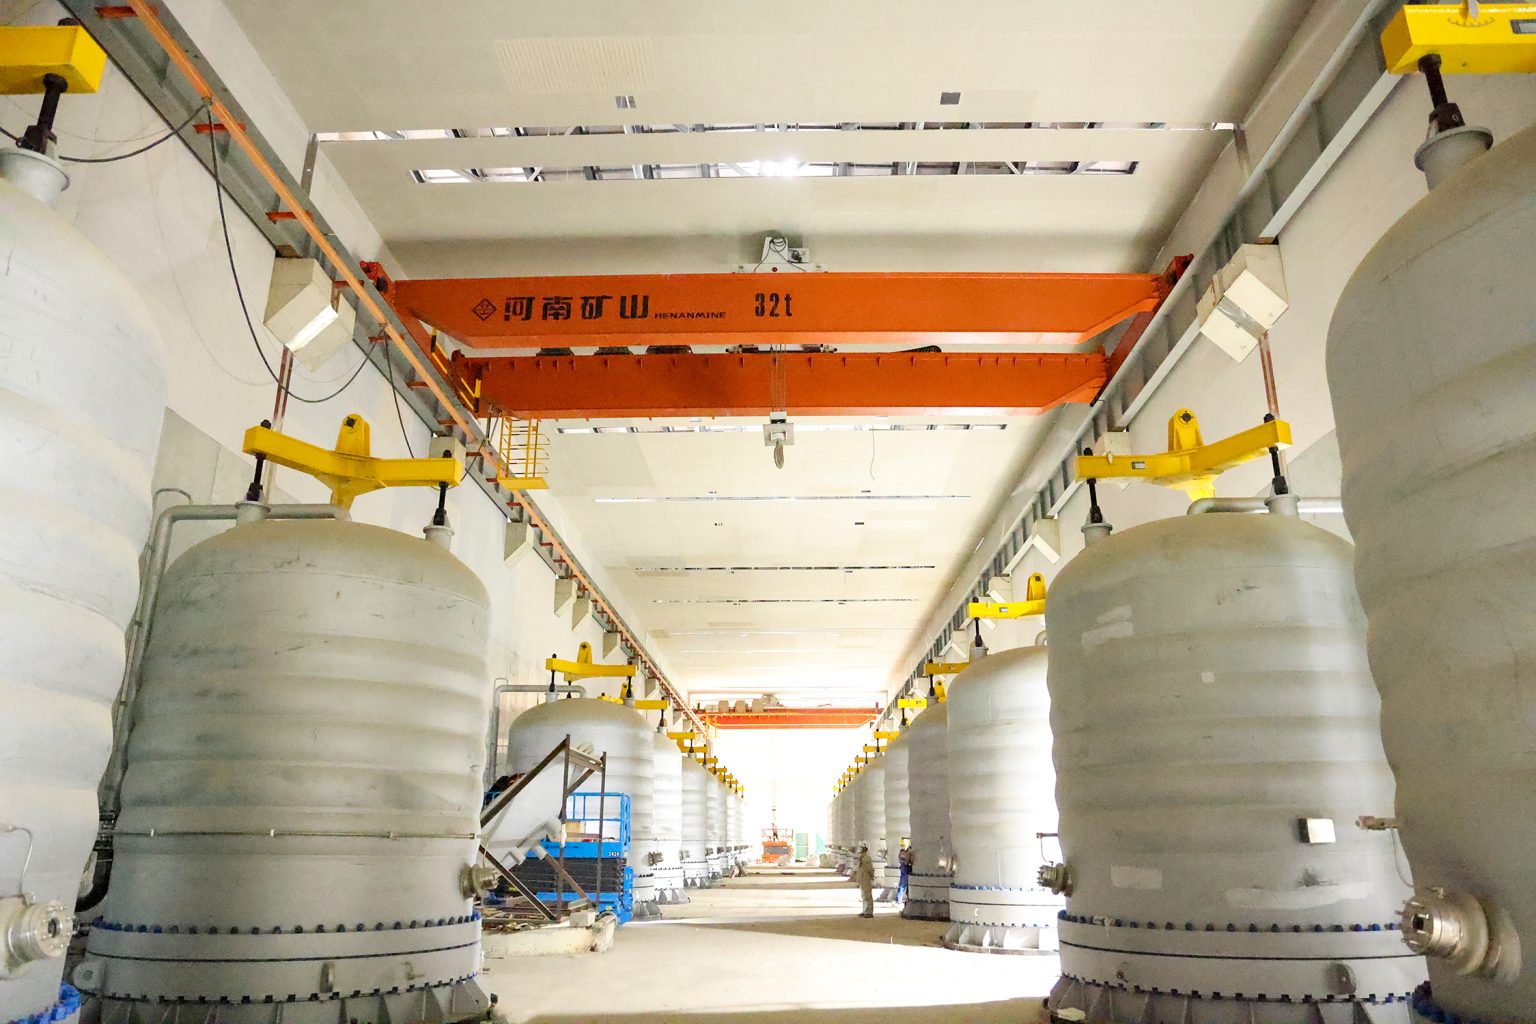
    overhead crane for workshop Henan Mine Crane Factory supply

     Quick Selection Checklist

    Finally, we will organize a simple checklist for you to check against when selecting, so that you can quickly clarify the requirements, avoid missing key parameters and save selection time:

    ✔ What is the maximum lifting load? (including spreader weight)

    ✔ What is the span and lifting height of the workshop? (accurate to centimeters)

    ✔ Is the lifting of raw materials, semi-finished products, or heavy equipment?

    ✔ How long is the crane used per day? (Frequency of use)

    ✔ Do you need high-precision positioning? (e.g. precision parts lifting, machine tool assembly)

    ✔ Is it a new workshop or a remodeling of an existing machine shop?

    ✔ Is there any special environment in the workshop? (high temperature, explosion-proof, dust, high humidity, etc.)

    ✔ What is the budget range? (including initial investment and long-term maintenance costs)

    FAQ

    What is the best crane for a workshop?

    There is no absolute best, only the most suitable. Light load, small workshop, choose single girder overhead crane, cost-effective, easy to operate; heavy load, continuous operation of the workshop, choose double girder overhead crane, good stability, strong carrying capacity; existing locomotive room, low headroom scenario, choose the suspension crane, installation flexibility, without destroying the original structure.

    What is the approximate price of workshop overhead cranes?

    There is no fixed standard for the price, which mainly depends on the load, span, lifting height, configuration and environmental requirements. You can tell us the workshop parameters and requirements, we give you an accurate quotation.

    Can a crane be installed in an existing locomotive workshop?

    Yes, you can. As long as a load-bearing assessment of the workshop structure is done first to confirm that the roof or floor can withstand the load of the crane, it can be installed. Most of the existing locomotive room remodeling, we will recommend suspension cranes or self-supporting cranes, do not have to destroy the original structure, the installation cycle is short, does not affect the normal production of the workshop. We Henan Mine Crane have rich experience in existing locomotive room remodeling, can provide one-stop survey, design, installation services.

    How long can the workshop crane be used?

    Under normal maintenance, single girder cranes can be used for 10-15 years, and double girder cranes can be used for more than 15-20 years. The key is to choose the right type and daily maintenance in place, we Henan Mine Crane will provide regular maintenance guidance, but also provide global spare parts supply to extend the service life of the equipment. For example, our cranes exported to Russia can still operate stably under the extreme cold environment of -40℃, and their service life can be more than 20 years.

    Henan Mine Crane Factory Custom

    Choosing an overhead crane is not just buying a piece of equipment, but also buying long-term peace of mind, efficiency and safety. It is not simply “the bigger the better” “the cheaper the better”, but to combine your lifting needs, workshop structure, frequency of use and environment, accurate matching.

    Henan Mine Crane has been in the crane field for decades, focusing on the research, development, production and sales of overhead cranes for workshop use. All of our products comply with international standards such as ISO, FEM, CMAA, etc., and support customized design, so that they can be adapted to the needs of different regions and types of workshops around the world.

    Regardless of which country you are in the world, whether it is a new workshop or the renovation of an existing machine shop, whether you need a 1-ton light crane or a 500-ton heavy crane, we can provide free on-site survey, selection consultation, layout design, as well as global installation and commissioning and after-sales guarantee.

    Send your workshop drawings and needs, we will provide you with free technical solutions and quotations within 24 hours, to help you avoid selection mistakes, choose the most suitable workshop overhead crane, help your production work efficiently and safely.
    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose an Overhead Crane for Frequent Start-Stop Operations

    How to Choose an Overhead Crane for Frequent Start-Stop Operations

    How to Choose an Overhead Crane for Frequent Start-Stop Operations

    In industrial scenarios such as metallurgical processing, assembly line transportation, and heavy-duty assembly, industrial bridge cranes have been in high-frequency start-stop operation conditions for a long time. Such high-frequency operation bridge cranes can start and brake repeatedly hundreds of times a day, which can easily cause motor overheating, brake wear, structural fatigue, positioning offset and other problems, greatly increasing the probability of failure and maintenance costs.The core reason for the premature aging and frequent downtime of most bridge crane equipment is not the quality defect of bridge crane equipment, but the use of ordinary light-load models in the selection of bridge cranes, which does not match the high-frequency operating conditions.Combining the start-stop operation characteristics to accurately match the parameters of the bridge crane, the configuration of the bridge crane and the operation and maintenance plan of the bridge crane is the key to ensuring the stable operation of the equipment, extending the service life of the equipment, and reducing production losses.

    Key Factors When Choosing a Crane

    The selection of bridge cranes with frequent start-up and stop conditions should not only focus on the rated lifting weight of bridge cranes, but also on the fatigue resistance, dynamic operating stability, and start-stop carrying capacity of the equipment.Conventional cranes focus on static load adaptation, while high-frequency start-stop bridge crane equipment needs to take into account dynamic impact, continuous cycle operation, thermal stability and braking reliability. This is the core selection standard for high-performance bridge cranes.The following four core elements are the core basis for selection, which directly determine the equipment failure rate and service life.

    Duty class and load capacity

    The working level and load capacity are the basic core of the selection of high-frequency start-stop bridge cranes, the key indicators of the adaptation of industrial bridge cranes to working conditions, and the key parameters that are most easily overlooked.According to the national standard GB/T 3811-2008, industrial bridge cranes are divided into eight working levels A1-A8. Different specifications of bridge cranes are adapted to different operating intensities. Different levels correspond to different operating frequencies, load states and fatigue life, and are fully adapted to the needs of different starting and stopping conditions.A1-A3 is a light-level work system, which is suitable for warehouse maintenance and spare hoisting scenarios with low average daily start-stop times and intermittent operations. It is completely unsuitable for high-frequency start-stop conditions. Forced use will quickly cause fatigue of the main beam, motor burning, and brake failure.

    A4-A5 is an intermediate work system, suitable for conventional production in ordinary workshops, with an average of 8 hours of uninterrupted operation per day, which can meet the needs of moderate start and stop.For high-frequency start-stop continuous operation scenarios, the A6-A8 heavy-duty work system must be selected. The total number of cycles designed for this type of equipment can reach up to 4 million times, and the structural safety factor and load-bearing fatigue strength are greatly improved, and it can withstand the dynamic impact of long-term repeated start-stop.The selection of load capacity must follow the principle of dynamic adaptation, and cannot only refer to the peak load.In high-frequency operations, the equipment can withstand the impact of variable loads for a long time. It is recommended to reserve 1.2-1.5 times the safe load margin to avoid structural deformation and component aging caused by frequent start and stop at full load.At the same time, it is necessary to distinguish between conventional operating loads and extreme loads, and take the daily high-frequency hoisting weight as the core selection basis, so as to eliminate the heavy-duty and high-frequency operation of small-level bridge cranes, and effectively extend the service life of Henan Mine Crane manufactured bridge cranes.

    Motor performance and braking system

    The motor and brake system are the core power and safety barriers for high-frequency start-stop operations of bridge cranes, as well as the core vulnerable system of bridge cranes under high-frequency operating conditions, and they are also high-failure components.Ordinary fixed-speed motors have a large current shock at the moment of start and stop, and the speed changes violently. Repeated start and stop will quickly cause the coil to heat up, the insulation layer to age, and the motor to burn down. It is completely unable to adapt to high-frequency operating conditions.For cranes that are suitable for frequent start-and-stop, special motors with high frequency resistance, high heat dissipation, and overload resistance must be selected. They have strong instantaneous overload capacity and continuous start-and-stop resistance, which can effectively reduce the impact of start-and-stop current and reduce heat accumulation.

    At the same time, the motor needs to be equipped with an independent heat dissipation structure to ensure temperature stability under long-term high-frequency operation and avoid thermal shutdown failures.The braking system is directly related to operation safety and equipment loss. It is strictly forbidden to use ordinary monolithic brakes in high-frequency start-stop conditions.Repeated opening and closing of conventional brakes will quickly cause problems such as brake pad wear, brake lag, and brake failure.Professional high-frequency start-stop cranes are equipped with wear-resistant hydraulic brakes or electromagnetic dual-braking systems as standard. The braking response speed is fast, the fit is stable, and the amount of wear is small. It can achieve accurate slow-stop, eliminate start-stop frustration and load shaking, and avoid structural shocks caused by emergency braking, greatly improving operation safety and component durability.

    Hoisting and traveling speed

    The reasonable matching of the lifting and operating speed of the bridge crane is the key to balancing the production efficiency of high-frequency start-up and stop conditions with the loss of bridge crane equipment.The speed is too fast, the start-stop impact is large, the load swing is serious, and the wear of components is accelerated.If the speed is too slow, it will directly reduce the transfer efficiency of the assembly line and affect the overall production capacity.The lifting speed needs to be adapted according to the attributes of the hoisting material: precision parts, fragile materials, and high-precision assembly scenarios. Priority should be given to the low-speed and smooth lifting mode to avoid material bumps and positioning deviations caused by start-stop shaking.For heavy-duty bulk materials and conventional batch transfer scenarios, medium and high-speed lifting can be selected to improve operational efficiency.

    The industry’s general adaptation standard is that the lifting speed of light-duty high-frequency equipment below 5 tons is adapted to about 8m/min, and heavy-duty equipment above 10 tons is adapted to low-speed parameters of 7m/min and below, ensuring stability is a priority.The operating speed of carts and trolleys also needs to be adjusted in a targeted manner.Under high-frequency start-stop conditions, the operating speed needs to support stepless speed regulation to achieve a smooth transition from low-speed start-up, uniform-speed operation, and gentle braking.For high-frequency operations in conventional workshops, the operating speed of the cart is recommended to be controlled at 20-30m/min, and the precision operation scenario can be lowered to 15-20m/min, which completely solves the problems of fuselage tremor, load offset, and track wear caused by frequent start and stop of bridge cranes, and improves the operating stability of bridge cranes.

    Crane Components for High-Frequency Operations

    The standard accessories of ordinary bridge cranes are only suitable for low-frequency intermittent operations, which cannot meet the operating needs of bridge cranes under high-frequency operating conditions, and cannot withstand the continuous impact and heat loss of high-frequency start and stop.To ensure the long-term stable operation of the equipment, it must be equipped with special core accessories for high-frequency working conditions, upgraded from multiple dimensions of transmission, braking, electronic control, and protection, and targeted to solve the pain points of high-frequency operations.

    Variable frequency drive systems

    Under the working conditions of hundreds of start-stop cycles per day, the frequency conversion system of Henan Mine Crane manufactured bridge crane can effectively stabilize the working current of the bridge crane motor, reduce the heat accumulation of the coil, and reduce the fatigue loss of the motor, reducer, main beam, and track.In addition, the high-quality frequency conversion system has overload protection, stall protection, and fault self-test functions, which can monitor the operating status of the equipment in real time, and warn of downtime in time when high-frequency operations are abnormal, so as to avoid major failures caused by the operation of the equipment with diseases, and greatly improve the operating stability and safety of the equipment. It is the core configuration for cost reduction and efficiency enhancement in high-frequency start-up and shutdown conditions.

    Hoist gearbox and mechanical brakes

    The hoist reducer and mechanical brake are the core transmission and braking components of the bridge crane, which determine the reliability of the high-frequency operation of the bridge crane. It can withstand alternating loads for a long time under high-frequency start-stop conditions, and has extremely high requirements for material accuracy, wear resistance, and fatigue resistance.Ordinary reducer gear accuracy is low, lubrication stability is poor, and repeated start and stop are prone to gear wear, abnormal noise, caton, transmission failure and other problems.The special hoist reducer for high-frequency working conditions adopts high-strength alloy gears and precision gear grinding technology. It has the characteristics of high wear resistance, impact resistance and low noise. It can withstand the transmission load of continuous and repeated start and stop. The transmission efficiency is stable, and it is not prone to gear failure, oil leakage and other failures.

    At the same time, it is equipped with a forced lubrication system to continuously supply oil to cool down during high-frequency operation to avoid excessive oil temperature and lubrication failure caused by high-speed circulating operation.The supporting special mechanical brakes use thickened wear-resistant brake linings and integrated brake structure. Compared with ordinary brakes, the wear-resistant life is increased by 2-3 times, the braking response is more accurate, and the opening and closing are more stable.The dual mechanical braking design can realize redundant protection, and the other group can intervene immediately when a single set of brakes fails, eliminating the safety hazards of sliding hooks and sliding in high-frequency start-stop operations of bridge cranes, and ensuring the safety of bridge crane operations.

    Electrical control and thermal protection

    The most common hidden fault in high-frequency start-stop operations is the overheating of the motor and electronic control system. Long-term heat accumulation will accelerate circuit aging, insulation failure, and component burning, greatly shortening the service life of the equipment.Therefore, a professional electronic control system and a perfect thermal protection mechanism are indispensable configurations for high-frequency bridge cranes to ensure long-term continuous operation of bridge cranes.The high-frequency dedicated electronic control system adopts a modular and integrated design, with a regular circuit layout and strong anti-interference ability. It can be adapted to frequent signal switching of high-frequency start and stop, eliminating signal delay, command confusion, malfunction and other problems.

    At the same time, it is equipped with an intelligent control system, which can accurately regulate the start-stop rhythm and operating speed, adapt to the operating needs of different working conditions, and improve the accuracy of hoisting and positioning.The thermal protection system adopts multiple protection design, and the core components such as motors, frequency converters, and reducers are equipped with temperature sensors, which can monitor the operating temperature in real time.When the temperature of the equipment exceeds the standard during high-frequency operation, the system will automatically trigger load reduction, cooling, early warning and even shutdown protection to avoid high temperature burning of the equipment from the root cause.At the same time, it is equipped with a forced cooling fan and a cooling duct structure to actively accelerate the cooling and ensure the stable operation of the equipment for 24 hours of continuous high-frequency operation.

    Selecting the Right Overhead Crane Configurationoverhead crane for frequent start-stop operations

    Depending on the fuselage structure and lifting mechanism configuration of the bridge crane, the high-frequency start and stop conditions of the adapted bridge crane are greatly different.The selection of single and double beam structure, electric hoist and hoist mechanism directly determines the carrying capacity, fatigue resistance, operating efficiency and applicable scenarios of the equipment.Combining workshop working conditions, lifting weight, operating frequency, and span height to select the appropriate configuration, in order to achieve the best price/performance ratio and the longest service life.

    Single girder vs. double girder

    Single-beam bridge cranes are lightweight in structure, lower in cost, and easy to install. They are commonly used models for high-frequency bridge cranes in small and medium-sized working conditions. They are suitable for small and medium-tonnage and medium-frequency start-up and stop-down conditions.For conventional workshops of 1-10 tons, with an average daily start-stop frequency of 100-200 times, and a small operating span, A5-A6 single-girder cranes can be used to meet the needs. The equipment has flexible operation, lower energy consumption, easy maintenance, and outstanding cost-effective advantages.

    The double-girder bridge crane adopts a double-girder load-bearing structure, which has stronger overall rigidity and better fatigue resistance. It is the preferred model for heavy-duty and high-frequency bridge cranes with higher carrying limits. It is the first choice for large tonnage, ultra-high frequency, and continuous operating conditions.For heavy loads of more than 10 tons, average daily start and stop of more than 200 times, 24-hour uninterrupted operation, and large-span plant scenes, A6-A8 double-girder cranes must be selected.Its structure has small deflection, no tremor in operation, can withstand long-term dynamic shocks, and will not cause deformation of the main beam or loosening of the structure due to frequent start and stop. The stability and safety far exceed that of single-beam models.

    Electric hoist vs. open winch

    The electric hoist lifting mechanism has a compact structure, light start and stop, and accurate positioning, which is suitable for small and medium-sized tonnage and refined high-frequency start and stop operations.It is widely used in machining, parts assembly, and light material transfer scenarios. It has the advantages of stable speed regulation, low noise, and simple operation and maintenance. It is suitable for high-frequency start-stop conditions of light and medium-load bridge cranes, and can effectively control the start-stop impact of bridge cranes to ensure the accuracy of precision hoisting operations.

    The open winch has high structural strength, high transmission torque, and strong impact resistance. It is specially designed for heavy-duty, high-strength, and ultra-high-frequency start-and-stop conditions.For large-tonnage and continuous cycle start-stop scenarios such as metallurgy, heavy industry, heavy equipment assembly, and bulk material transfer, the hoist lifting mechanism can withstand continuous heavy-duty shocks, and is not prone to slippage, wear, and transmission failure. The stability of continuous operation is stronger, and the safety of heavy-duty start-stop is higher. It is the core configuration of high-frequency bridge crane operations in heavy industry, which greatly improves the operating stability of heavy-duty bridge cranes.

    Customized crane specifications

    Standardized bridge crane parameters are difficult to adapt to all complex high-frequency start-up and shutdown conditions. Henan Mine Crane manufactured customized bridge cranes can be accurately adapted to special production scenarios. Customized parameters are the key to ensure the adaptability of equipment for special workshop environments and special operating needs.Professional manufacturers can customize the core parameters of the equipment in all directions according to the actual working conditions of users to accurately match the needs of high-frequency operations.Customizable content includes exclusive work level upgrade, frequency conversion speed regulation parameter adjustment, start-stop buffer program optimization, precise matching of lifting/operating speed, thermal protection system upgrade, high temperature and dustproof and waterproof configuration, long-span reinforced structure, non-standard lifting height, special track adaptation, etc.For example, high-temperature workshops can be customized with high-temperature motors and sealed protective structures, high-dust workshops can be equipped with dust-proof and noise-reducing configurations, and ultra-high-frequency assembly lines can optimize the start-stop logic to further reduce equipment losses and improve operating efficiency.

    Maintenance Requirements for Frequent Start-Stop Cranes

    High-frequency start-stop bridge cranes have been in a state of high-load and high-cycle operation for a long time. The loss rate of such industrial bridge cranes is much higher than that of conventional equipment, and the loss rate of components is much higher than that of ordinary cranes. Conventional maintenance standards cannot meet their operating needs.Targeted special maintenance can greatly reduce the probability of failure, delay the aging of components, effectively extend the overall service life of equipment, and reduce enterprise operation and maintenance costs.

    Reducing motor and brake wear

    Motors and brakes are the components with the fastest loss in high-frequency operations, and they are also the core focus of maintenance.In daily operation and maintenance, it is necessary to regularly clean the motor cooling air duct and check the operating status of the cooling fan to avoid dust accumulation and heat accumulation and aging caused by poor heat dissipation.At the same time, the motor insulation resistance and coil temperature are regularly tested, and the circuit aging and virtual connection problems are investigated in time to prevent the instantaneous current impact of start and stop from burning down the motor.The brake system needs to be inspected daily, focusing on the degree of wear of the brake lining, brake clearance, hydraulic system pressure, and electromagnetic coil status.The lower lining of high-frequency operation is a vulnerable part, and it is necessary to replace the worn-out parts in time, and adjust the brake clearance regularly to ensure stable and accurate braking.At the same time, regularly clean up the dust of the brake mechanism and fill it with special lubricating grease to prevent brake caton, lag, and failure, reduce the start-stop loss of the bridge crane from the root cause, and extend the service life of the core components of the bridge crane.

    Inspection and preventive maintenance

    For high-frequency start-stop cranes, it is necessary to establish a preventive maintenance system, abandon the passive operation and maintenance mode of post-mortem maintenance, and take regular inspections, early investigations, and early maintenance as the core to avoid sudden failures.

    • Daily pre-shift inspection: check the start and stop operation status of the equipment, whether there is abnormal noise and tremor, whether the braking is sensitive, whether the electronic control indicator light is normal, and deal with minor abnormalities in a timely manner.
    • Weekly special inspections: detect the fastening status of the main beam, end beam, and track, investigate the hidden dangers of structural fatigue, check the oil level and oil quality of the reducer lubricating oil, and replace the deteriorated lubricating oil.
    • Monthly in-depth inspection: verify the parameters of the frequency conversion system, the sensitivity of the thermal protection system, the operating current of the motor, and the performance of the braking system, and tighten the wiring and connecting bolts of the whole vehicle.
    • Annual comprehensive flaw detection: non-destructive flaw detection of the main beam, welds, and transmission components to investigate fatigue cracks and structural deformation, and eliminate major safety hazards.

    Extending crane service life

    If you want to maximize the service life of high-frequency start-stop bridge cranes, you need to standardize the operation and maintenance process of bridge cranes, and you need to start with standardized operation, regular maintenance, adaptation of working conditions, and multi-dimensional comprehensive control of parts replacement.First of all, strictly standardize the operation process, eliminate savage start-stop, emergency stop, and overload operation, and reduce unnecessary mechanical shocks and load losses.Secondly, adapt the operating frequency in strict accordance with the operating conditions of the equipment, and do not use the equipment under excessive or overloaded loads.

    At the same time, we insist on regular replacement of the original supporting wearing parts to avoid the problem of insufficient matching and increased loss caused by inferior accessories.Regularly optimize the operating parameters of the equipment, fine-tune the frequency conversion speed regulation and start-stop buffer parameters according to the operating frequency, and adapt to actual working conditions.Do a good job of dust-proof, waterproof, and rust-proof protection of the equipment, and install exclusive protective devices under harsh working conditions to delay the aging of the equipment in all directions, and increase the service life of the high-frequency start-stop crane by more than 30%.

    How to Choose a Reliable Overhead Crane Manufacturer

    The precise selection of bridge cranes adapted to the working conditions of Henan Mine Crane manufactured is inseparable from the technical support of professional manufacturers. Bridge cranes with high-frequency working conditions have higher design process requirements.High-frequency start-stop cranes are customized industrial equipment. The manufacturer’s design capabilities, production technology, quality inspection standards, and after-sales system directly determine the stability, durability, and use experience of the equipment.Choosing a reliable source manufacturer is the core prerequisite for avoiding selection errors, reducing failure rates, and ensuring long-term stable operations.

    Engineering design and customization

    High-quality crane manufacturers must have professional working condition survey and customized engineering design capabilities, and can issue exclusive selection plans and equipment design drawings one-on-one according to the span of the user’s workshop, lifting height, lifting tonnage, average daily start-stop frequency, and operating environment.In view of the high-frequency start-and-stop conditions of bridge cranes, the professional design team will upgrade the structural strength of bridge cranes in a targeted manner, optimize the start-and-stop control logic, match the dedicated frequency conversion and heat dissipation system, and avoid various hidden dangers of high-frequency operations from the source of the design.

    At the same time, it has mature non-standard customization capabilities, which can solve the adaptation problems of special working conditions and special sites, refuse to standardize equipment and hard-set complex working conditions, and ensure that each equipment accurately matches the user’s high-frequency start-stop operation requirements, so as to achieve efficient, stable and low-loss operation.

    Factory testing and quality assurance

    High-frequency start-stop cranes have extremely high requirements for production technology and quality inspection standards. Ordinary small factories lack special testing processes, and the equipment is prone to high-frequency operation failures after leaving the factory.Reliable source manufacturers have a perfect standardized production system and strict factory inspection process, and have professional load testing, start-stop cycle testing, temperature testing, and braking performance testing equipment.

    All Henan Mine Crane manufactured special cranes for high-frequency working conditions will undergo tens of thousands of simulated start-stop cycle tests, overload tests, and continuous thermal stability tests before leaving the factory, and comprehensively test the tolerance performance of motors, brakes, frequency conversion, and structures to ensure that bridge crane equipment can be adapted to long-term high-frequency start-stop operations, and ensure that the bridge crane’s factory quality is up to standard.At the same time, it has a complete qualification certification and quality assurance system, strictly follows the national standard production, and the quality of the equipment can be traced and guaranteed.

    After-sales service and spare parts

    The maintenance frequency of high-frequency start-stop bridge cranes is high, and the replacement of wearing parts is frequent. Perfect service is the guarantee of the long-term operation of bridge cranes, and a perfect after-sales service system is an important guarantee for the long-term stable operation of equipment.High-quality manufacturers have a national after-sales team that responds quickly, and can provide one-stop services for on-site investigation, installation and commissioning, regular maintenance, and emergency repair of faults. For sudden failures in high-frequency operations, they can respond quickly and solve them quickly, minimizing the loss of production.

    At the same time, it has sufficient reserves of original parts, and core parts such as motors, brakes, frequency conversion modules, and reducers can be supplied quickly to avoid long-term downtime caused by out-of-stock parts.In addition, professional manufacturers will provide customers with free operation and maintenance training on working conditions, guide operators to standardize use, daily inspections, and basic maintenance, and help enterprises reduce equipment failure rates, extend equipment service life, and achieve long-term cost reduction and efficiency gains.

    Henan Mine Crane Factory Custom

    The core logic of the selection of bridge cranes with frequent start-up and stop conditions is based on the adaptation of working conditions as the core, focusing on anti-fatigue, stable start-stop, and strong protection, and abandoning the single selection misunderstanding of only looking at tonnage.From the working level, power brake configuration, speed parameters, special accessories, fuselage structure, to late maintenance and manufacturer screening, every link directly affects the safety, efficiency and service life of the equipment.

    The high-frequency special bridge crane adapted to working conditions can not only perfectly adapt to the continuous start-stop operation requirements of the bridge crane, greatly reduce the failure and shutdown rate and maintenance costs, but also ensure the production efficiency of the workshop for a long time and create sustainable value for the enterprise.If you have crane customization, selection, and transformation needs for high-frequency start-stop conditions, you can consult us at any time. Henan Mine Crane Factory provides one-to-one exclusive working condition solutions.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose an Overhead Crane for Continuous Production Lines

    How to Choose an Overhead Crane for Continuous Production Lines

    For 24-hour continuous operation of assembly line production, bridge cranes will be deeply embedded in the production process, directly affecting the operating efficiency and safety level of the production line.The continuous carrying capacity and fatigue resistance of the crane under such working conditions are much higher than that of conventional intermittent operating environments.Many companies only pay attention to basic specifications when purchasing, and do not combine the actual working condition assessment of long-term high-frequency operations. After being put into use, they often encounter unstable operation and frequent failures, which not only disrupt the rhythm of production, but also bring about continuous increase in maintenance expenses. Therefore, the selection should be based on the actual operating status of the entire production line, and a comprehensive assessment should be completed starting from the job requirements.

    What Makes Overhead Cranes Different for Continuous Production Lines

    The core difference between Henan Mine Crane manufactured bridge cranes for continuous production lines and ordinary workshop cranes is that the operating logic is fully adapted to the uninterrupted production mode of the mass production line.Ordinary cranes are mainly intermittent, on-demand start-stop, and low-frequency operations, with high fault tolerance.The continuous production line crane needs to fit the fixed beat of the production line, high-frequency cycle operation, and long-term continuous operation, and the requirements for equipment stability, response speed, wear resistance, and safety redundancy have been greatly improved.The following explains the basis for differentiated selection from the four core dimensions.

    Production demands

    The core production requirements of continuous production lines are standardization, beat-based, and uninterrupted mass production, which requires the crane to be fully adapted to the production rhythm of the production line and cannot become a bottleneck in production capacity.In scenarios such as automobile manufacturing, steel structure processing, warehousing assembly lines, heavy industry mass production, food and chemical automation production lines, material handling, workpiece loading and unloading, and finished product transportation are all deeply bound to the production line.Ordinary cranes can only meet the needs of scattered and temporary handling, with slow start-stop response and poor operating stability, and cannot match the beat of a fixed production line.The bridge crane adapted to the continuous production line can design a fixed operating trajectory and start-stop rhythm according to the production line capacity, so as to achieve accurate synchronization with the assembly line process, and ensure that every material transfer is in line with the production schedule, and there will be no waste of energy consumption by idling equipment, nor will there be problems of material accumulation and process caton. It is fully adapted to the core needs of large-scale continuous production.

    Load frequency

    The frequency of load operation is the key indicator to distinguish between ordinary cranes and continuous production line cranes.The average number of daily operations of ordinary workshop cranes is small and the interval is long, and the equipment has sufficient heat dissipation, cushioning, and fatigue recovery time.The cranes of continuous production lines are high-frequency circulating operating equipment, with an average number of lifting, transshipment, and blanking times of hundreds or even thousands of times per day, and they are in a state of repeated start-stop and continuous force for a long time.High-frequency operation will cause continuous fatigue loss to the main beam, walking mechanism, hoist system, motor, brake and other core components of the crane.Therefore, cranes for continuous production lines must adopt thickened main beams, strengthened transmission structures, high-temperature motors and wear-resistant brake accessories to eliminate component deformation, overheating, brake failure and other problems under high-frequency operations, and ensure long-term stable operation under high-frequency load conditions.

    Workflow needs

    The workflow of a continuous production line has the characteristics of closed loop, automation, and coherence. Cranes are an indispensable part of the production line process, not independent operating equipment.Traditional cranes rely on manual control, their operating efficiency varies from person to person, and their operating errors are large, and they cannot be adapted to standardized assembly line processes.The Henan Mine Crane manufactured bridge crane adapted to continuous working conditions can customize the operating logic according to the production line process, support fixed-point start-stop, fixed-point blanking, and fixed-track operation, and can perfectly connect the upper and lower processes.Whether it is the warehousing and transportation of raw materials, the loading and unloading of processed workpieces, the handling of finished products out of the warehouse, or the flow of materials between processes, it can accurately match the assembly line operation process, open up the closed loop of material handling on the production line, and avoid process caton and production delays caused by manual operation errors. Adapt to an automated and standardized continuous production workflow.

    Key Specifications to Check Before Choosing an Overhead Crane

    The selection of cranes for continuous production lines cannot be judged by experience alone, and must rely on accurate equipment parameters to match working conditions.The core technical parameters directly determine the operating capacity, adaptability, service life and operating stability of the equipment, which is the basis for avoiding selection errors and ensuring the continuous operation of the production line.The following six core parameters are the key indicators that must be checked when selecting a company.

    Load capacity

    The rated load is the basic core parameter of the crane, but it is strictly forbidden to accurately match the maximum material weight for the selection of continuous production lines.Due to continuous operation, there are problems such as material weight fluctuations, instantaneous impact loads, and long-term fatigue loss of equipment. If the rated load is the same as the actual load, the long-term full-load operation of the equipment will accelerate aging and can easily cause safety failures.For continuous mass production conditions, it is recommended to reserve 1.2~1.5 times the load redundancy when selecting the model.For example, the conventional maximum hoisting weight of a production line is 5 tons, and a 6-ton or 7.5-ton crane needs to be selected to effectively buffer the instantaneous load pressure of high-frequency operations, avoid long-term full-load and overload operation of equipment, and extend the service life of equipment. At the same time, it should meet the needs of fine-tuning material specifications and temporary heavy-duty operations in the production process.

    Lifting height

    The lifting height determines the vertical space of the crane’s operation, which directly affects the flexibility and adaptability of the material transfer of the production line.When selecting the type, you cannot only refer to the headroom height of the workshop. It needs to be calculated comprehensively in combination with the height of the production line equipment, the height of the material stacking, the height of the workpiece processing, and the safe reserved distance.

    Material transfer in continuous production lines is frequent. If the lifting height is insufficient, there will be problems such as material bumping equipment, inability to complete cross-process transfer, and limited working space.If the lifting height is too redundant, it will increase the weight of the equipment and operating energy consumption, and reduce operating efficiency.The precisely matched lifting height can ensure the rapid lifting and smooth transfer of materials, and adapt to the compact and efficient operation rhythm of the assembly line.

    Crane span

    Henan Mine Crane manufactured crane span refers to the distance from the center of the cart track at both ends, which determines the horizontal operation coverage of the equipment and is directly adapted to the overall layout of the production line.Continuous production lines are mostly long strips and large-scale layout, and the selection of span directly affects whether there are no dead ends in the global material handling of the production line.When selecting the type, it must be determined strictly based on the track spacing of the workshop, the area covered by the production line operation, and the maximum horizontal distance of material transfer.If the span is too small, part of the production line area cannot be covered, and secondary transportation is required, interrupting the continuous production cycle.If the span is too large, the deflection of the main beam will increase, the stability of the equipment will decrease, and the operation and maintenance costs will increase.The precisely matched span can realize efficient handling of the whole production line without dead ends and ensure production continuity.

    Travel speed

    The operating speed includes the walking speed of the cart, the operating speed of the trolley and the lifting speed, which are the core parameters that match the production beat of the production line.Ordinary cranes are slow and non-adjustable, and are only suitable for low-speed and intermittent operations.The continuous production line has extremely high requirements for handling efficiency and beat synchronization.The high-speed adjustable operating speed can be dynamically adjusted according to the production line capacity: the transportation can be accelerated during the peak period of mass production to avoid material accumulation.The precision workpiece processing stage can run smoothly at low speed to prevent material shaking and offset.At the same time, it is equipped with frequency conversion and speed control technology to achieve stable start-stop and stepless speed change, avoid inertial shocks caused by high-speed start-stop, protect equipment and workpieces, and perfectly adapt to the rhythmic operation needs of continuous production lines.

    Duty class

    The working level is the core index of crane selection in continuous production lines, and it is also the most easily overlooked parameter.The working level directly defines the crane’s operating frequency, continuous working time, and fatigue tolerance.Ordinary low-level cranes are only suitable for occasional operations and intermittent operation conditions, and cannot be adapted to 24-hour continuous mass production scenarios at all.Continuous production lines must use medium and high-level working-level cranes, which can withstand high-frequency, long-term, and cyclic operations, effectively resist equipment fatigue and loss, and reduce the probability of failure and shutdown. It is the key to ensure the long-term continuous and stable operation of the production line.

    Control system

    The control system determines the operating accuracy, operating stability and automation adaptation capabilities of Henan Mine Crane manufactured cranes, and is the core hub connecting cranes and continuous production lines.The traditional manual control system is cumbersome to operate, has low accuracy, and relies on labor, and cannot be adapted to automated continuous production.Cranes adapted to continuous production lines mostly use frequency conversion control systems and PLC intelligent control systems, which support manual control, semi-automatic fixed-point operation, and fully automatic program operation in various modes.It can accurately control the start and stop, speed, and positioning, and the error is controlled at the millimeter level. At the same time, it can be connected to the production line automation system to realize the automation of the whole process of material transfer without manual intervention, which is perfectly adapted to the unmanned and continuous production needs of the assembly line.

    overhead crane

    How to Match Crane Duty Class to Production Workload

    The precise matching of crane work level and production load is the core of avoiding equipment overload and aging, frequent failures, downtime and missed work.The working level is not up to standard, even if the basic parameters such as load and span are all matched, the equipment cannot withstand the high-intensity operation of a continuous production line.Below, the load matching method is explained in detail from the four dimensions of working condition classification, operating cycle, working time, and downtime risk.

    Duty classifications

    The working level of domestic bridge cranes is divided into eight levels A1~A8 according to national standards. The higher the level, the stronger the fatigue resistance, high-frequency operation, and continuous operation ability of the equipment.A1-A3 are light-grade working conditions, suitable for scattered workshops, occasional hoisting, and low-frequency operation scenarios, and are not suitable for continuous production lines at all.A4-A5 are intermediate working conditions and are suitable for production lines with conventional mass production and regular daily operations.A6-A8 are heavy-duty and extra-heavy-duty working conditions, and are specially adapted to 24-hour uninterrupted, high-frequency circulation, and heavy-duty continuous production lines.For high-load continuous working conditions such as mass production of auto parts, continuous processing of steel structures, automated warehousing assembly lines, and mass production of heavy industry equipment, high-level cranes of A6 and above must be selected to adapt to the needs of high-intensity operations in terms of equipment structure, accessory material, and transmission system.

    Operating cycles

    The number of operation cycles is the core basis for determining the matching of working conditions, and refers to the complete number of lifting-transshipment-blanking-resetting operations of the crane every day and month.The operating cycle of the continuous production line has the characteristics of immobility, high frequency and uninterrupted, and the number of daily cycles far exceeds the operating standards of ordinary workshops.Low-level cranes are designed to withstand low cycle times, and long-term high-frequency cycle operations will quickly cause structural fatigue, wear of accessories, and motor aging.The high-level crane has been strengthened and designed to withstand more than one million stable operating cycles, and can be adapted to the high-frequency cycle conditions of continuous production lines for a long time to ensure the long-term accuracy and stability of the equipment.When the enterprise selects the type, it can accurately correspond to the crane work level according to the average number of daily operation cycles of the production line.

    Working hours

    The effective daily working time is an important reference for matching working conditions.Ordinary workshop cranes work for no more than 4 hours a day, and there is a lot of standby and idle time.The continuous production line is divided into long-term operating modes such as 12-hour two-shift reversal and 24-hour three-shift reversal, and the equipment has almost no downtime and rest time.A1-A3 class cranes are only suitable for short-term intermittent operations.A4-A5 is suitable for regular operations of 8-12 hours a day.A6-A8 class cranes are designed for 24-hour uninterrupted continuous operation. The core components are optimized for high temperature resistance, fatigue resistance, and continuous load resistance. They can maintain stable operation for a long time without overheating, caton, failure and shutdown due to long-term work. Problems.

    Downtime risks

    The biggest hidden danger caused by the mismatch of working conditions is that high-frequency downtime and failures directly interrupt the continuous production cycle.If the low-level crane is forcibly adapted to high-intensity continuous working conditions, there will be a series of failures such as motor burning, brake failure, deformation of the main beam, wear and fracture of the wire rope, and frequent downtime for maintenance.For continuous production lines, every equipment shutdown will cause the entire production line to shut down, material backlog, order delays, labor and energy consumption waste, and bring huge invisible economic losses.High-level cranes with accurate matching working conditions have extremely low failure rates and long maintenance cycles, which can minimize the risk of downtime and ensure continuous and stable mass production of production lines around the clock.

    Which Overhead Crane Configuration Fits Your Production Line?

    Different production line layout, material specifications, and operation requirements correspond to different crane configuration plans.The differentiated combination of main beam structure, operation mode, hoist configuration, and automation scheme directly determines the operating efficiency, adaptability, and cost performance of the equipment.The following four core configuration options cover the adaptation scenarios of most continuous production lines.

    Single vs. double girder

    Henan Mine Crane manufactured single-girder bridge crane has a lightweight structure, lower cost and lower energy consumption. It is suitable for light-load, medium-load, medium- and small-span continuous production lines. It is commonly used in mass production lines of light industry, electronics, and small parts. The frequency of operation is medium, the load weight is low, and the cost-effective advantage is significant. It can meet the needs of conventional continuous handling, simple operation and maintenance, and low cost.The double-girder bridge crane adopts a reinforced structure with double main beams, which has stronger bearing capacity, higher stability and better fatigue resistance. It is suitable for heavy-duty, long-span, and ultra-high-frequency continuous production lines, such as heavy-duty manufacturing, steel structure processing, large-scale mold mass production, heavy-duty material transfer and other scenarios.The double-girder structure can be equipped with a larger tonnage hoist and a higher configuration automation system. It does not deform or shake during long-term high-intensity operations, and its stability far exceeds that of single-girder cranes. It is the first choice for heavy-duty continuous production lines.

    Top vs. under running

    The up-running crane track is installed on the top of the main beam of the plant. It has strong load-bearing capacity, large working space, and is suitable for large-span and heavy-duty continuous production lines. It has a stable structure and strong impact resistance. It is suitable for large-scale factories and high-load mass production conditions. It is the mainstream configuration of industrial continuous production lines.The track of the down-running crane is suspended under the ceiling of the plant, with a lower overall height and a smaller footprint. It is suitable for continuous production lines with low headroom and light material transfer in the plant, such as precision machining, food and medicine, and light storage assembly lines.The equipment is lighter in operation and less noisy, and is suitable for compact workshop layout, but the load and span are limited, making it unsuitable for heavy-duty and high-intensity operations.

    Single vs. multiple hoists

    The single hoist crane has a simple structure, easy control and low failure rate. It is suitable for continuous production lines with single material and single process transportation. It can meet the needs of conventional one-to-one material handling, low operation and maintenance costs, and stable operation. It is the basic configuration of small and medium-sized continuous production lines.The multi-hoist crane can be equipped with two or more electric hoists, supports two modes of synchronous operation and independent operation, and can simultaneously complete multi-station material transfer, multi-point hoisting of large workpieces, and partitioned handling of light and heavy materials. It is perfectly adapted to multi-process, multi-station, and complex continuous production lines.It can greatly improve the handling efficiency, match the production capacity requirements of high-yield lines, and solve the problems of insufficient efficiency and lagging production capacity of single hoist operations.

    Automated options

    Automated configuration is the core upgrade direction of modern continuous production line cranes, completely getting rid of the limitations of manual control, and realizing unmanned, precise, and beat-based operations.The basic automation configuration is frequency conversion speed regulation + fixed-point start and stop, which can realize standardized operations on fixed trajectories and adapt to conventional assembly line production.The high-end automation configuration includes functions such as PLC intelligent control system, scan code positioning, trajectory memory, automatic correction, remote monitoring, and unattended operation. It can be connected to production line management systems such as MES and ERP, and automatically adjust the work rhythm according to the production plan to realize the automation of the whole process of material transfer.Greatly improving production efficiency, reducing labor costs, and avoiding human operation errors are standard for intelligent continuous production lines.

    Safety and Reliability Requirements for Continuous Crane Operation

    Continuous production line cranes operate at high frequency and for a long time, and the risk of safety hazards and equipment loss is much higher than that of ordinary intermittent operation equipment.Safety protection configuration and reliability design are the bottom line to ensure the continuous operation of equipment without failure and zero accidents.A perfect safety system can effectively avoid hoisting accidents, equipment damage, and production line shutdowns. The following six core safety configurations are essential.

    Overload protection

    Overload protection is the core safety protection device, which can monitor the lifting weight of the crane in real time.In the continuous production process, it is inevitable that the material is overweight and the loading error will occur. If there is no protection, the instantaneous overload will directly cause the main beam to deform, the wire rope to break, the motor to burn down, and even cause hoisting accidents.The high-precision overload protection device can provide real-time early warning, automatic power failure, and forced stop of operations to eliminate overload operation, avoid the risk of overload from the source, protect the core structure of the equipment and the safety of production line operations, and adapt to long-term uninterrupted operation scenarios.

    Limit switches

    The travel limit switch includes lifting limit, cart walking limit, and trolley walking limit, which is used to limit the maximum operating range of the crane.In the continuous automated operation mode, the equipment runs in a long-term cycle, which is prone to problems such as over-stroke operations, material collisions, and equipment bumps.The limit switch can automatically stop and reset in reverse when the equipment is running to the safety boundary, so as to prevent out-of-range operations, avoid collision damage to equipment, workpieces, and production line equipment, and ensure that every cycle operation is completed within a safe range to achieve safe and stable operation around the clock.

    Anti-collision systems

    Multiple cranes operating in parallel, intensive workshop equipment, and compact production line layout are common scenarios for continuous production lines, and collisions between cranes and cranes and plant equipment are extremely prone to occur.The collision will not only damage the crane equipment, but also directly disrupt the production cycle and cause the production line to shut down.The anti-collision system uses infrared sensing, laser detection and other technologies to monitor the distance of peripheral equipment in real time, automatically slow down and stop urgently at close range, effectively avoid the risk of collision, adapt to multi-equipment, high-density continuous production conditions, and ensure the stable operation of the equipment cluster.

    Variable frequency drives

    The frequency conversion drive system is the core configuration to ensure the stability of continuous operation.Traditional cranes start and stop stiffly and have a large inertial impact. Long-term operation will exacerbate structural wear and material shaking and offset, affecting production accuracy.Frequency conversion drive can achieve stepless variable speed, soft start, soft stop, smooth start and stop without impact, effectively reduce equipment mechanical fatigue, reduce accessories wear, and extend equipment service life.At the same time, it can accurately match the running beat of the production line, take into account the operating efficiency and operating stability, and adapt to long-term high-frequency continuous operation.

    Maintenance needs

    Low maintenance cost and easy maintenance design are important manifestations of the reliability of cranes in continuous production lines.Continuous production conditions do not allow long-term downtime for maintenance, so when selecting models, priority must be given to equipment with modular structure, universal accessories, and convenient maintenance.High-quality special cranes for continuous production lines, the core components can be disassembled and independently overhauled, the maintenance process is simple, the cycle is long, and the failure rate is low. The production line can be used for short-term material replacement and rest time to complete rapid maintenance without long-term downtime.At the same time, the equipment comes with a fault self-inspection system, which can monitor the operating status in real time, warn of faults in advance, realize preventive maintenance, completely avoid sudden failures and shutdowns, and ensure continuous and efficient production of the production line.

    Henan Mine Crane Factory Custom

    The selection of bridge cranes for continuous production lines should not only focus on basic indicators such as load and span, but also fit the actual working conditions of high frequency, continuous and fixed rhythm of the production line.The stability of the long-term operation of the equipment directly determines whether the production line can produce smoothly and continuously, and it is also related to the overall operating cost.Choose the right adapted model, the material transfer is smoother, the production beat is no longer dragged down by the hoisting link, the order loss caused by sudden downtime is greatly avoided, and the long-term maintenance expenditure is also reduced.Henan Mine Crane Factory is deeply engaged in the field of lifting equipment. It can customize highly durable, high-safety and redundant bridge cranes according to the actual situation of the on-site production line, and use stable and reliable handling hardware to escort enterprises to mass production on a large scale around the clock.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose an MG Double Girder Crane for Port Terminals

    How to Choose an MG Double Girder Crane for Port Terminals

    How to Choose an MG Double Girder Crane for Port Terminals

    Port terminals move some of the heaviest, most awkwardly shaped cargo in any industry containers, bulk commodities, project cargo, steel coils often in salt air, high wind, and around-the-clock schedules. Choosing the wrong crane doesn’t just slow down throughput; it creates a maintenance and safety liability that compounds for the next 15–20 years.

    The MG double girder crane is the workhorse of choice for this environment: a box-girder gantry crane built for high capacity, wide spans, and outdoor durability. But “MG” covers a huge range from a 5-ton yard crane to a 500-ton bulk handler and picking the right one means working through capacity, span, duty class, corrosion protection, and control systems in the right order.

    This guide walks through that selection process step by step, so you can specify a crane that matches your actual operation instead of overpaying for capability you don’t need or underbuying a crane that wears out in three years.

    What Is an MG Double Girder Crane?

    An MG double girder crane is a full-gantry crane built with two parallel box-type girder beams spanning between vertical support legs, which travel on ground-level rail tracks. The “MG” designation specifically denotes the double-girder, box-girder-frame gantry configuration, as distinct from single-girder (MH) or semi-gantry designs.

    The double-girder box structure matters because it distributes load across two beams instead of one, which increases stiffness, allows a wider span, and reduces beam deflection under heavy or off-center loads. Main parts of an MG double girder gantry crane include the main girder, support legs, a crane traveling mechanism, and a trolley system.

    While MG double girder gantry cranes are widely used for outdoor cargo handling and heavy lifting, many port terminals also deploy RTG cranes, rail-mounted gantry cranes (RMG), overhead cranes, and electric hoists to meet different material handling requirements across container yards, warehouses, and maintenance facilities.

    MG Crane vs. Other Port Crane Types

    Before locking in an MG gantry crane, confirm it’s actually the right category for your terminal. Ports commonly use four crane types, and confusing them leads to over- or under-specification.

    • MG double girder gantry crane:general-purpose, ground-rail-mounted, used for mixed cargo, bulk, break-bulk, and lower-density container yards. Most flexible and typically the most cost-effective for mixed operations.
    • RMG (rail-mounted gantry) crane:a purpose-built variant of the double girder gantry crane, optimized specifically for high-density container stacking in dedicated container terminals, usually with taller legs and automation-ready controls.
    • RTG (rubber-tyred gantry) crane:similar footprint to an MG/RMG crane but mounted on rubber tires instead of rails, trading some stability for mobility across a yard without fixed rail infrastructure.
    • STS (ship-to-shore) crane:a much larger, quay-mounted crane used specifically to load/unload containers directly from vessels; this is a different equipment category entirely and not a substitute for a yard-level MG crane.

    If your terminal handles standardized containers at high density with tight stacking requirements, an RMG variant may outperform a general MG crane. If you need to move equipment around the yard without rail infrastructure, an RTG may fit better. If your operation is mixed cargo bulk, breakbulk, occasional containers a standard MG double girder gantry crane is usually the right and most economical choice.

    Step 1: Define Your Load Profile

    Start with what you’re actually lifting, not a round number. <cite index=”11-1″>Load capacity is a critical specification defining how much weight the crane can safely lift, and capacities typically range from 5 tons to over 500 tons</cite> across the MG product line.

    Key questions to answer before you spec capacity:

    1. What is your heaviest single lift?Not the average load, the maximum. Container spreaders, grabs, and hook attachments each add dead weight that eats into usable capacity.
    2. What cargo mix are you handling?Standard ISO containers, bulk commodities via grab, breakbulk via hook, or a mix that requires interchangeable attachments.
    3. What’s your growth margin?Specifying exactly to today’s heaviest lift leaves no room if cargo mix shifts. Most terminals build in a 10–20% capacity buffer.

    Rate the crane to your worst-case lift plus margin, not your typical-day average undersizing here is the single most expensive mistake to fix after installation.

    Step 2: Determine Span and Lifting Height

    Span and lifting height are dictated by your yard geometry, not by the crane catalog. Span refers to the distance between the two vertical legs of the crane, and common spans for double girder gantry cranes range from 5 meters to 35 meters</cite>, though custom spans are available for specific operational layouts.

    To size this correctly:

    • Measure yard width:including rail gauge, plus clearance for trucks or vehicles passing beneath the crane legs.
    • Account for stacking height:container yards stacking 3–5 high need more lifting height clearance than single-layer bulk storage.
    • Consider leg configuration:U-type legs create more clearance underneath for large loads and vehicle passage, which matters heavily for container and heavy equipment terminals, while A-type legs are simpler and lower-cost for straightforward yard use.

    Undersizing span forces awkward truck routing around the crane footprint; oversizing span adds unnecessary steel weight, foundation cost, and wind load exposure.

    Step 3: Select the Right Duty/Working Class

    Duty class (also called working class or service class) determines how much wear and stress the crane’s mechanisms are engineered to absorb over its design life and it is the single most commonly under-specified factor in port crane procurement.

    Duty class in three systems (FEM / ISO / CMAA):

    Intensity China (A-class) Europe (FEM) USA (CMAA)
    Light duty A1–A4 1Dm/1Cm Class A–B
    Moderate duty A5–A6 1Bm Class C
    Heavy duty A7 2m Class D
    Severe/continuous duty A8 3m Class E–F

    A1 to A4 are considered light duty, A5 and A6 fall into the medium duty category, A7 is classified as heavy duty, and A8 represents extremely heavy duty under the Chinese classification system commonly used by MG crane manufacturers.

    For port terminals specifically, most operations land in A6 or A7: higher duty classifications are typically applied in harsh environments or where automation and continuous production are prioritized, both of which describe standard port operating conditions. A yard crane used only occasionally for overflow storage might justify A5, but a terminal crane running multiple shifts with frequent lifts should be specified at A6 or above.

    Duty class isn’t just a paperwork classification it directly drives maintenance load. A5 cranes might require routine maintenance monthly or quarterly, while A6 cranes need more frequent inspections, often weekly, along with faster wear-out of critical components like wire ropes and brakes. Factor this into staffing and maintenance budgets before you commit to a duty class, not after.

    Step 4: Plan for the Marine Environment

    Port cranes operate in one of the harshest corrosion environments in industrial equipment salt spray, humidity, and temperature swings accelerate steel degradation far faster than an indoor or inland industrial crane experiences.

    Specify these protections up front rather than retrofitting them later:

    • Structural coating system:hot-dip galvanizing or multi-layer epoxy coatings are standard for outdoor port structures; marine-grade high-strength steel with a defined corrosion allowance is preferable for splash-zone exposure.
    • Electrical enclosure rating:offshore and marine equipment typically adopts IP56/IP67 protection grades</cite> for enclosures exposed to spray and washdown; inland equipment can often use a lower rating, but ports generally should not.
    • Cab and control environment:sealed, climate-controlled operator cabs extend both operator comfort and electronics lifespan in humid, salty air.
    • Inspection cadence:corrosion-prone environments need shorter coating inspection intervals than the manufacturer’s default schedule; budget for this as an operating cost, not a one-time spec item.

    Skipping marine-grade protection to save on upfront cost is one of the most common false economies in port crane procurement steel replacement and unplanned downtime almost always cost more than the coating premium.

    Step 5: Choose Trolley, Hoist, and Lifting Attachment

    The trolley and hoist configuration determines what the crane can actually pick up, and it should match your cargo mix from Step 1, not be an afterthought.

    • Open winch trolley: an open winch is a common lifting mechanism in double girder gantry cranes, consisting of a winch drum, motor, and gearbox housed in an open frame, which allows easy maintenance and inspection of components. This design suits heavy-duty applications requiring frequent maintenance access.
    • Hoist trolley (crab): a more compact, enclosed alternative better suited to standardized, repetitive lifts with less need for open-frame servicing.
    • Attachment type:hook for general and breakbulk cargo, grab bucket for bulk commodities, container spreader for standardized ISO containers, and electromagnetic lifters for suitable ferrous cargo.Versatility is a key advantage of the MG type crane, as it can be equipped with a variety of lifting devices such as electric hoists, grabs, and disks to meet different operating needs.

    If your terminal genuinely handles mixed cargo types, specify quick-change attachment capability up front retrofitting a single-purpose crane for a second cargo type later is far more expensive than building in flexibility at purchase.

    Step 6: Evaluate Control, Automation, and Safety Systems

    Modern MG port cranes are no longer just structural steel and a motor control and safety systems are now a major differentiator in both productivity and risk management.

    Look for these systems as standard on any port-grade specification:

    • Equipped with variable frequency drive system (VFD), it can realize smooth acceleration and deceleration of equipment, effectively reduce wear and tear of mechanical structure, and greatly improve energy saving efficiency of equipment operation.
    • Equipped with cab local control and remote control dual mode, it can combine the operation vision conditions and site layout, flexibly select the control mode, and adapt to the operation requirements of multiple scenarios.
    • Equipped with anti-collision and anti-swing intelligent system, effectively avoid the risk of damage caused by cargo collision and shaking, and at the same time relieve the workload of high-frequency repeated operation of operators and improve the stability of operation.
    • Standard overload protection device, lifting height limiter and rail clamp, all-round to meet the terminal open air, windy complex conditions of crane foundation safety operation standards, to build a solid line of operation safety.
    • Equipped with intelligent fault diagnosis and remote monitoring function, it is the mainstream standard configuration of A6/A7 cranes, which can monitor the operation status of equipment in real time, predict maintenance requirements in advance, effectively avoid shutdown problems caused by equipment failure, and ensure operation continuity.

    None of these systems are optional extras for a serious port operation they should be treated as baseline requirements in your procurement specification, not upsell items.

    Cost Factors and Total Cost of Ownership

    Sticker price is a poor way to compare MG crane quotes, because capacity, span, duty class, and attachment type all move price independently and the ongoing maintenance burden of a higher duty class can outweigh the upfront cost difference over the crane’s operating life.

    When comparing quotes, evaluate:

    • Main structure cost: The main structure cost of equipment is determined by rated load and span.Increasing the size of the box main beam and increasing the height of the outriggers will increase the amount of steel used and directly increase the overall manufacturing cost of the equipment.
    • High-level operating mode configuration cost: equipment adopts A6/A7 high-level working level supporting parts, including brakes, wire ropes, drive systems and other core accessories.This configuration has a higher initial purchase cost, but is designed for the wear characteristics of port high-frequency and high-intensity operations, and is suitable for port heavy load conditions.
    • Anti-corrosion protection configuration cost: equipment equipped with marine-grade anti-corrosion protection scheme, through high-end marine coating, sealing protection structure, high-quality special steel configuration to strengthen anti-corrosion performance.Although the initial investment is increased, the high steel maintenance and renovation costs in the medium term of equipment use can be effectively avoided.
    • Maintenance inspection costs: high-level cranes need to perform higher-frequency inspection maintenance processes, resulting in continuous manual operation and maintenance costs.Cost accounting shall cover the full cycle of 5 to 10 years, and it is not allowed to calculate the single cost of equipment purchase.
    • Intelligent control and automation configuration cost: inverter drive, remote diagnosis, anti-swing and other intelligent systems have high investment in the early stage, but they can shorten the operation cycle, reduce downtime, and achieve efficiency and cost reduction throughout the life cycle of the equipment.

    The lowest quote is rarely the lowest total cost once duty class mismatch, corrosion retrofit, or capacity undersizing show up three to five years into operation.

    Common Buyer Mistakes to Avoid

    • The model is selected according to average load instead of maximum operation load, which leads to no safety redundancy and insufficient operation safety under heavy load condition.
    • In order to reduce the initial cost and reduce the working level of equipment, it will accelerate the wear of parts, improve the failure shutdown rate, and significantly increase the full-cycle maintenance cost.
    • Under high salinity and splash corrosion conditions, marine grade corrosion prevention scheme is not configured, which is easy to cause premature corrosion of the structure and cause early maintenance and rectification.
    • The goods category is complicated, but the fixed single accessory is selected, and the adaptability is poor. In the later stage, additional cost shall be invested for transformation and upgrading.
    • The automation and safety system is regarded as optional configuration, which is not included in the basic standard of continuous operation port, and cannot meet the requirements of high-frequency and high-intensity operation.
    • The model category is not confirmed according to the operation scenario, and the high-density container yard is mismatched with the general gantry crane (MG) or the rail-mounted gantry crane (RMG), resulting in insufficient matching degree of equipment working conditions and limited operation efficiency.

    Conclusion

    Port MG double beam gantry crane selection can not only refer to load parameters, but also combine with model working conditions, structural parameters, corrosion protection and electric control system comprehensive customization optimization.Scientific selection can improve quality and efficiency, reduce cost and prolong life, effectively reduce downtime loss and improve yard capacity by relying on the whole life cycle value of equipment.

    Henan mine crane can customize all kinds of port lifting equipment and intelligent lifting system, adapt to port, logistics, shipyard, heavy industry and other scenarios, provide load analysis, working condition accounting, structure design and other one-stop technical services, accurately adapt to various operating environments.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose an Intelligent Warehouse Crane for a Logistics Center?

    How to Choose an Intelligent Warehouse Crane for a Logistics Center?

    How to Choose an Intelligent Warehouse Crane for a Logistics Center?

    Logistics centers are running out of two things at once: floor space and workers. As order volumes climb and warehouse footprints stay fixed, more operators are turning to an intelligent warehouse crane to solve both problems at the same time ; going vertical while cutting the manual labor needed to move goods.

    This guide walks through what an intelligent warehouse crane actually is, the components that make it work, the types available, the ten factors that should drive your decision, the software and safety features that matter most, how to match equipment to your physical layout, the mistakes that most often derail a selection process, and the ROI logic that justifies the investment — so you can choose a system that fits both today’s operation and tomorrow’s growth.

    What Is an Intelligent Warehouse Crane?

    Definition and Working Principle

    Henan Mine Crane manufactured intelligent warehouse crane is automated lifting and handling equipment that stores, retrieves, and transports goods within a warehouse with minimal human intervention. What separates it from a conventional crane is the layer of control, sensing, and software that lets it operate autonomously rather than under constant manual direction.

    Most intelligent warehouse cranes function as the mechanical core of an automated storage and retrieval system (AS/RS). Rather than an operator directing every lift, the crane receives a task from a control system, calculates the fastest path, positions itself automatically, and confirms completion back to the software, all without manual input. The operator’s role shifts from “driving” the equipment to monitoring exceptions and confirming that the system is running as expected.

    Three capabilities define this behavior:

    • Automatic positioning:the crane locates the correct rack position using sensors rather than operator judgment
    • Automatic lifting and traveling:hoist and travel motions are computer-controlled, not manually driven
    • Automatic inventory handling:every movement is logged, so the system always knows what is stored where, down to the individual bin or pallet position

    This last point is worth emphasizing: in a manual warehouse, inventory accuracy depends on a human correctly scanning, recording, or remembering a location. In an intelligent warehouse crane system, the location is generated and confirmed by the machine itself, which removes an entire category of human error from the process.

    Main Components

    An intelligent warehouse crane is built from several interdependent subsystems, each of which contributes to overall reliability and performance:

    • Crane bridge:the structural frame that spans the aisle or bay and carries the mast and hoist assembly
    • Hoisting mechanism:the motor, drum, and rope or chain assembly that lifts loads vertically
    • Intelligent control system:the onboard computer (typically a PLC or industrial controller) that executes tasks and coordinates motion across all axes simultaneously
    • Servo motors and frequency converters:precision drives that control speed, acceleration, and positioning far more tightly than a standard induction motor
    • Positioning sensors:laser or encoder-based systems that confirm exact location along the rail and mast
    • Barcode/RFID readers:used to identify and verify individual loads before storage or retrieval
    • Communication system:wireless or trailing-cable links to the central control network that transmit task assignments and status updates
    • WMS interface:the software connection that turns warehouse-level orders into crane-level tasks, and reports back inventory movements in real time

    Each of these subsystems can fail independently, which is why vendor support and spare parts availability matter as much as the initial specification.

    Typical Applications

    Intelligent warehouse cranes are used across a range of facility types, each with different priorities and constraints:

    • E-commerce fulfillment centers:high SKU counts, fast turnover, and heavy peak-season volume swings
    • Third-party logistics (3PL):flexible storage that must accommodate multiple clients with different product profiles
    • Manufacturing warehouses:feeding components directly to production lines on a just-in-time basis
    • Cold storage warehouses:automation reduces worker exposure to extreme temperatures and improves throughput in low-visibility conditions
    • Automotive parts warehouses:high accuracy needed for dense parts catalogs with thousands of similar-looking SKUs
    • Pharmaceutical distribution centers:traceability, controlled handling, and audit-ready inventory records are often regulatory requirements, not just efficiency goals

    Why Are Intelligent Warehouse Cranes Becoming the Standard in Logistics Centers?

    Higher Warehouse Storage Density

    Because Henan Mine Crane manufactured intelligent cranes operate with millimeter-level positioning accuracy, they can run in narrow aisles that would be unsafe for a forklift or manually operated crane. Narrower aisles mean more racking fits into the same building footprint. Combined with the ability to fully maximize vertical warehouse space, often reaching heights well beyond what a forklift mast can safely achieve, this typically allows facilities to store significantly more inventory without expanding the building itself.

    Faster Order Fulfillment

    Automated material handling removes the delays inherent in manual operation: walking to equipment, manually navigating aisles, and manually confirming locations. Cranes travel direct, computer-calculated paths with minimal wasted motion, and because they don’t need breaks, shift changes, or rest periods, many systems support continuous 24/7 operation, a meaningful advantage during peak season surges when order volume can spike several times over baseline. For operations running compressed fulfillment windows, same-day or next-day shipping commitments, for example — the ability to run unattended overnight shifts can be the difference between meeting a cutoff and missing it.

    Improved Inventory Accuracy

    Every movement an intelligent crane makes is logged automatically. Real-time inventory updates and automatic location confirmation remove the manual data entry errors that come with paper-based or scanner-dependent processes, which is one of the most consistently cited benefits in industry case studies. This matters most in operations with strict cycle-count requirements or regulatory traceability obligations.

    Lower Operating Costs

    Automation also cuts time required for repetitive handling tasks by reducing manpower requirements and using accurate, sensor-guided movements, meaning lower levels of product damage and improved equipment use than manual handling fleets, which often sit idling between tasks or need a multitude of operators on multiple shifts in order to function.

    Enhanced Workplace Safety

    Crane accidents, whether mobile or stationary are heavily skewed to human error miscalculated clearances, fatigue, blind spots when operating cranes manually. Intelligent systems are minimizing this risk by automatic detection of obstacles, and collision avoidance, as well as remote monitoring for abnormal conditions abnormal vibration or torque, increased motor temperature that prevent incidents before they happen, rather than after.

    Intelligent Warehouse Crane

    Types of Intelligent Warehouse Cranes

    Choosing the right category is the first real decision point, since each type is engineered for a different load profile, aisle configuration, and warehouse layout.

    Crane Type Best For Typical Load Typical Aisle Width
    Stacker crane High-rise AS/RS pallet warehouses Pallets, up to several tons 1.4–1.8 m
    Mini load crane Small parts, cartons, bins Light loads, under ~500 kg 0.8–1.2 m
    Double-deep stacker crane Higher-density layouts, deeper racks Pallets 1.4–1.8 m
    Multi-shuttle system High-throughput distribution centers Mixed, high cycle rates Varies (shuttle-based)
    Customized solution Oversized or non-standard cargo Varies Varies

    Stacker Crane

    The workhorse of most high-bay warehouse operations, a stacker crane runs on fixed rails within a single aisle to place and retrieve pallet storage loads at height, often exceeding 20–30 meters in high-bay AS/RS installations. Cycle times for a well-specified stacker crane commonly fall in the range of one to two minutes per single-cycle pallet movement, though this varies with lift height and travel distance.

    Mini Load Crane

    Built for smaller, lighter items, cartons, plastic bins, and small parts, mini load cranes are common in parts distribution and e-commerce piece-picking operations where SKU density matters more than raw load weight. Because the loads are lighter, mini load systems can often achieve faster cycle times than pallet-handling equivalents.

    Double-Deep Stacker Crane

    By reaching two positions deep into a rack instead of one, this configuration increases storage density in warehouses with suitable layouts, though it adds complexity to retrieval sequencing, the crane may need to relocate the front pallet before accessing the one behind it, which increases average cycle time even as it improves overall space utilization.

    Multi-Shuttle Crane Systems

    For high-throughput logistics centers and large-scale e-commerce distribution, multi-shuttle systems combine crane movement with independent shuttle carriers that travel within the rack structure itself, decoupling vertical lifting from horizontal placement. This architecture can hit far higher aggregate cycle rates than a single stacker crane alone, at the cost of a more complex control system and a higher initial investment.

    Customized Intelligent Warehouse Crane Solutions

    Facilities with heavy-duty storage, unusual environmental conditions, or oversized cargo handling needs often require a purpose-engineered system rather than an off-the-shelf configuration. This is common in industries handling coils, molds, or oversized industrial components that don’t fit standard pallet or bin dimensions.

    In practice, most logistics centers end up combining more than one crane type within a single facility rather than standardizing on a single configuration. A distribution center might run mini load cranes for a fast-moving small-parts zone alongside standard stacker cranes for bulk pallet storage, with a multi-shuttle system reserved for the highest-velocity SKUs. Mapping which product categories belong in which zone, based on velocity, weight, and dimensions, is a useful exercise before finalizing equipment counts and types.

    10 Key Factors to Consider When Choosing an Intelligent Warehouse Crane

    Selecting the right system means matching ten interdependent variables to your operation, get these right, and the rest of the buying process becomes straightforward.

    1. Warehouse Dimensions: Building height, rack height, aisle width, and available installation space set the physical envelope every other decision must fit inside. A crane that is mechanically ideal on paper is useless if it cannot physically be installed within your existing structural clearances, so a site survey should happen before, not after, equipment is specified.
    2. Load Capacity:Assess maximum load weight, typical average load, and realistic future expansion requirements,undersizing capacity is one of the costliest mistakes to correct later, since it often requires structural rework rather than a simple component swap. It’s also worth understanding standardized duty classifications at this stage: systems such as CMAA (Class A through F), FEM, and ISO 4301 rate cranes by how intensely they can be used based on load percentage and cycle frequency. Selecting a crane rated for occasional light service but operating it at near-continuous heavy-duty cycles is one of the fastest ways to shorten equipment life.
    3. Lifting Height:Confirm the maximum storage level the crane must reach and the total travel distance per cycle, since both affect cycle time,a crane that must travel further vertically on every cycle will inherently move fewer pallets per hour than one serving a shorter rack, all else being equal.
    4. Operating Speed:Hoisting speed, traveling speed, fork extension speed, and positioning accuracy together determine how many cycles the crane can complete per hour. These specifications should be evaluated together rather than individually, since a crane with a very fast travel speed but slow fork extension may not deliver the throughput gain its top-line speed rating suggests.
    5. Storage Throughput:Model expected pallets per hour, especially during peak operating periods, against realistic order processing requirementsrather than average-day volume alone. Many operators size equipment to average daily volume and then discover it cannot keep pace during seasonal peaks, throughput modeling should always be based on the busiest sustained period the operation expects to face, not the annual average.
    6. Automation Level:Decide whether the operation needs semi-automatic assistance,where an operator still confirms or triggers key actions, or fully automatic, lights-out warehouse capability, where the crane operates without any human presence in the aisle. The software and safety requirements differ substantially between the two, and retrofitting from semi-automatic to fully automatic later is typically far more expensive than specifying the correct level upfront.
    7. Software Integration:Confirm compatibility with your WMS, Warehouse Control System (WCS), ERP, and any existing IoT connectivity,a crane that can’t talk to your systems creates a manual bottleneck regardless of its mechanical capability. This is frequently the single most underestimated line item in a crane procurement budget, since integration work often requires custom middleware development rather than an out-of-the-box connection.
    8. Positioning Accuracy:Compare laser positioning, encoder systems, and RFID technologyoptions, since accuracy requirements scale with how tightly you plan to pack your racks. A facility running standard single-deep pallet racking has more tolerance for positioning variance than one running narrow-aisle or double-deep configurations, where a few centimeters of error can mean a failed placement.
    9. Energy Efficiency:Search for regenerative braking, VFDs and otherwise low energy consumption designs that will really make a difference in operating cost over a number of years of operation. Regenerative braking especially will inject a meaningful proportion of energy expended during slowing back into your power system, especially when multiplied up for the hundreds of cycles a day a crane might undertake.
    10. Maintenance Requirements:Evaluate remote diagnostics, predictive maintenancecapability, spare parts availability, and the vendor’s service support network before signing — this factor is consistently underweighted during purchasing decisions, yet it directly determines how much unplanned downtime the operation will experience over the equipment’s service life. Henan Mine Crane manufactured crane with excellent specifications but a distant, unresponsive service network can cost more in lost throughput during a single extended outage than the entire annual maintenance budget for a better-supported alternative.

    Intelligent Features That Matter Most

    Beyond the core mechanics, the software layer is what actually delivers on the “intelligent” label:

    • Automatic route optimization:calculates the fastest travel path for each task in real time, adjusting dynamically as other tasks are added to the queue
    • AI-based task scheduling:sequences multiple pending tasks to minimize total cycle time, often batching nearby storage and retrieval operations to reduce empty travel
    • Real-time equipment monitoring:gives operations teams live visibility into crane status, current task, and performance metrics through a dashboard rather than relying on periodic manual checks
    • Predictive maintenance:analyzes vibration, temperature, and motor load data to flag component wear before it causes downtime, shifting maintenance from a fixed calendar schedule to an as-needed basis
    • Automatic fault diagnosis:speeds up troubleshooting when an issue does occur by identifying the likely failure point rather than requiring a technician to manually isolate it
    • Cloud-based data management:centralizes performance data across multiple cranes or sites, which is particularly valuable for operators managing several distribution centers under one operations team
    • Digital twin technology:allows layout changes and throughput scenarios to be simulated before physical implementation, reducing the risk of costly design mistakes discovered only after installation

    Safety Features Every Intelligent Warehouse Crane Should Have

    Automation reduces certain risks, but it introduces its own safety-critical dependencies. A properly specified system should include:

    • Anti-collision system to prevent contact with racking, other equipment, or personnel, typically using a combination of laser scanning and software-enforced exclusion zones
    • Load monitoringto detect and respond to overload conditions in real time, halting operation before a mechanical failure can occur
    • Emergency stop functionsaccessible both locally at the crane and remotely from a central control room
    • Overspeed protectionon hoist and travel motions, which prevents runaway conditions in the event of a control system fault
    • Rope and hoist monitoringto catch wear before failure, since wire rope and chain degradation is a leading cause of catastrophic crane incidents
    • Obstacle detectionfor both fixed and moving objects in the crane’s path, including personnel who may enter the aisle unexpectedly
    • Redundant safety controlsso a single sensor or component failure doesn’t create an unsafe condition, critical safety functions should never depend on a single point of failure

    How to Match the Crane with Your Warehouse Layout

    Even the right crane type will underperform if it isn’t matched to the physical facility. Before finalizing a purchase, confirm:

    • Rack configuration:single-deep, double-deep, or shuttle-compatible racking each require different crane capabilities and control logic
    • Warehouse ceiling height:actual clearance versus theoretical lift height, accounting for sprinkler systems, lighting, and structural beams that may reduce usable height
    • Floor flatness:rail-mounted systems have tight tolerance requirements, and an out-of-spec floor can require costly remediation before installation
    • Material flow design:how goods physically move from receiving to storage to shipping, since the crane’s aisle position and orientation should minimize unnecessary cross-warehouse travel
    • Inbound and outbound frequency:peak-hour load versus average daily load, which determines whether a single crane per aisle is sufficient or whether multiple cranes or a shuttle system are needed
    • Future warehouse expansion:whether the layout can accommodate additional aisles, a taller rack structure, or additional cranes later without a full system redesign

    Common Mistakes to Avoid When Selecting an Intelligent Warehouse Crane

    Procurement teams that skip due diligence on these points tend to regret it within the first operating year:

    • Choosing based only on initial price:the cheapest quote rarely reflects total lifecycle cost, and a lower-spec system often requires earlier replacement or more frequent repair
    • Ignoring software compatibility:a mechanically excellent crane is still a bottleneck if it can’t integrate with your WMS, forcing manual workarounds that erase much of the automation benefit
    • Underestimating future throughput growth:sizing for today’s volume alone often forces an early retrofit that costs significantly more than specifying adequate headroom from the start
    • Selecting insufficient load capacity:a common and expensive error, especially when product mix changes over time and average pallet weight increases beyond original assumptions
    • Overlooking maintenance and service support:remote systems with no local service network create long downtime windows that can outweigh any upfront cost savings within the first significant breakdown
    • Neglecting operator training:even highly automated systems need trained staff for oversight, exception handling, and safety response; treating the crane as fully “hands-off” from day one is a common cause of avoidable incidents

    How Intelligent Warehouse Cranes Improve ROI

    The financial case for automation tends to rest on a handful of measurable outcomes, and evaluating them together, rather than any single metric in isolation, gives the clearest picture of payback timing:

    • Reduced labor costs:fewer operators needed for repetitive handling tasks, particularly valuable in labor markets where warehouse staffing has become increasingly difficult
    • Increased warehouse capacity:higher storage density within the same building footprint, which can defer or eliminate the need for a facility expansion
    • Faster order processing:shorter cycle times translate directly into fulfillment speed, which matters increasingly as customer expectations around delivery windows tighten
    • Reduced inventory errors:automatic tracking reduces costly stock discrepancies that otherwise require manual cycle counts and write-offs
    • Lower product damage:sensor-guided handling reduces mishandling incidents compared with manual forklift or crane operation
    • Long-term operational savings:energy-efficient drives and predictive maintenance reduce both utility and repair costs over the equipment’s service life

    Documented deployments in steel and electronics warehousing have reported storage density gains and labor cost reductions in the double- and triple-digit percentage range, underscoring why automation investment has accelerated across logistics operators facing tight labor markets. When modeling ROI internally, it’s worth building a simple comparison: total installed cost of the intelligent crane system against the combined savings from reduced headcount, reduced facility expansion need, and reduced error-related write-offs over a five- to ten-year horizon. Most operators find that the software integration and training costs — not the crane hardware itself — are the largest variable in how quickly that payback is realized, which is another reason software compatibility deserves early attention in the selection process rather than being treated as an afterthought.

    It also helps to separate ROI into “hard” and “soft” categories when presenting the business case internally. Hard savings, reduced headcount, reduced facility square footage, reduced error write-offs, are straightforward to quantify and typically drive the initial payback calculation. Soft benefits, improved workplace safety, better customer satisfaction from faster and more accurate order fulfillment, and greater resilience during labor shortages, are harder to put a dollar figure on but often prove just as important once the system has been operating for a year or more. Facilities that track both categories from the start tend to make a stronger case for expanding automation into additional aisles or zones later.

    Why Choose a Customized Intelligent Warehouse Crane Solution?

    Standard configurations work for many facilities, but Henan Mine Crane Factory customized intelligent warehouse crane solution is often the better fit when requirements fall outside typical parameters:

    • Tailored to warehouse dimensions:engineered to your exact height, span, and aisle constraints rather than forcing your facility to fit a standard product line
    • Optimized for industry requirements:cold chain, pharmaceutical, or heavy industrial applications each have distinct needs around temperature rating, traceability, or load handling that off-the-shelf systems may not fully address
    • Scalable automation:designed to add aisles, shuttles, or throughput capacity as the operation grows, avoiding a full system replacement down the line
    • Integration with existing systems:built to connect with legacy WMS or ERP platforms rather than forcing a costly and disruptive system replacement just to accommodate the new crane
    • Long-term technical support: a dedicated service relationship rather than a one-time equipment sale, which matters considerably given how much lifecycle cost is tied to maintenance and downtime

    Frequently Asked Questions (FAQ)

    What is the difference between a warehouse crane and a stacker crane?

    A warehouse crane is the broad equipment category, bridge, gantry, and jib cranes all qualify. A stacker crane is a specific type built for automated storage and retrieval, running on fixed rails within a single aisle.

    How much weight can an intelligent warehouse crane lift?

    It varies by application: mini load cranes typically handle 50–500 kg, pallet stacker cranes commonly handle 500–1,500 kg per pallet, and customized heavy-duty systems can exceed several tons.

    Can warehouse cranes integrate with WMS and ERP systems?

    Yes. Most intelligent warehouse cranes connect to a WMS through a Warehouse Control System layer, and many also exchange data directly with ERP and MES platforms.

    How accurate are intelligent warehouse cranes?

    Laser and encoder-based positioning systems typically achieve placement accuracy within a few millimeters, enabling narrow-aisle and double-deep storage configurations.

    How long does installation usually take?

    A single-aisle stacker crane with WMS integration commonly takes several weeks to a few months from delivery to commissioning; multi-shuttle systems across multiple aisles take longer.

    How often should intelligent warehouse cranes be maintained?

    Most manufacturers recommend daily visual checks, monthly inspection of brakes and structural components, and a full annual service, supplemented by remote monitoring where available.

    Are intelligent warehouse cranes suitable for cold storage warehouses?

    Yes, with modifications such as low-temperature-rated motors, lubricants, sensors, and condensation-resistant electrical enclosures.

    What is a crane duty class and why does it matter?

    Duty class is a standardized rating, such as CMAA A through F, FEM, or ISO 4301 — that describes how intensely a crane can be used based on load percentage and cycle frequency. Selecting the wrong duty class for your actual usage pattern accelerates wear and increases the risk of premature failure.

    Do intelligent warehouse cranes require a dedicated IT infrastructure?

    Most installations require a stable local network, a server or cloud instance to run the Warehouse Control System, and integration middleware to connect with the existing WMS or ERP. The scale of this infrastructure depends on the number of cranes and the level of automation deployed.

    Henan Mine Crane Factory Custom

    Selecting the most appropriate intelligent warehouse crane involves weighing up the dimensions of the warehouse, load requirements, throughput, degree of automation, software integration, safety, energy efficiency and long term maintenance requirements. The most suitable solution is not the one with the highest specifications, but the one that is designed to work with your workflow today while allowing the capacity and capabilities to grow into the future. This considered approach can often result in a more efficient warehouse and cost effective automation solution.

    Every logistics center is different, with various storage configurations, levels of handling and automation objectives. That’s why there is no “one size fits all” answer. If you are designing a new automated warehouse or considering automating an existing one, a knowledgeable crane manufacturer will help you find the most effective system for your intelligent warehouse crane. Partnering with a specialist offering everything from crane design to software integration, installation and commissioning, and support for the life of your warehouse will ensure you get a high quality, dependable, easy-to-operate system that meets your needs and continues to support your growth.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose an Intelligent Overhead Crane for an Unmanned Workshop?

    How to Choose an Intelligent Overhead Crane for an Unmanned Workshop?

    How to Choose an Intelligent Overhead Crane for an Unmanned Workshop?

    In Henan Mine Crane do intelligent bridge crane sales and technical support these years, I witnessed a lot of factories from the traditional manual workshop to unmanned transition.

    Industry 4.0 wave, more and more manufacturing enterprises began to build intelligent, unmanned production environment, and the bridge crane as the core equipment of the workshop material handling, the pressure of transformation also came.

    Traditional overhead cranes are highly dependent on manual operation, which not only require specialized operators, but are also prone to positioning deviation and uneven efficiency, which are not suitable for unmanned workshop.

    The emergence of intelligent overhead crane for unmanned workshop solves this pain point – it can realize automated operation, accurate positioning and digital integration, and become the indispensable core equipment for unmanned workshop.

    Many purchasing managers are easily confused when selecting models, not knowing where to start. Today, I will combine Henan Mine Crane’s hands-on experience in serving customers around the world, and use common language to help you clear up the core logic of selection and avoid the pits that are easy to step on.

    What Is an Intelligent Overhead Crane?

    Definition

    Many people think that an Intelligent Overhead Crane is an automation module added to a traditional crane, but this is not the case.

    It is a complete set of automated lifting system, the core configuration is indispensable, including AI-based control algorithms, high-precision positioning equipment, automatic anti-shaking technology, sensor safety system, PLC control architecture, as well as with the MES, ERP system integration capabilities.

    The intelligent overhead crane for unmanned workshop provided by Henan Mine Crane to global customers will be customized according to the workshop scenarios, such as strengthening the load monitoring in heavy-duty workshops, and improving the positioning accuracy in precision manufactured workshops to ensure that it is suitable for the actual operational needs.

    In short, it is not a simple superposition of “traditional crane + automation”, but an “intelligent handler” that can autonomously complete the work, interface with the production system, and ensure safety, which is the core reason why it can be adapted to unmanned workshop.

    How It Differs from Traditional Overhead Cranes

    Feature Traditional Crane Intelligent Crane
    Operation Manual Automated / Remote
    Positioning Operator-controlled Millimeter precision
    Anti-sway Manual skill Automatic suppression
    System Integration Standalone Integrated with MES/ERP
    Suitable for Unmanned Workshop No Yes

    The difference between the two, from the operation logic to the system integration, there is a fundamental difference, I have organized a simple comparison, we will understand at a glance:

    To give a practical example, the traditional crane positioning all depends on the operator’s experience, the error is often in a few centimeters or even a dozen centimeters; while the millimeter-level positioning of the intelligent overhead crane can accurately put the material into the designated position, without the secondary adjustment of manpower.

    There is also system integration, the traditional crane is running independently, can not dock the workshop production system; and intelligent overhead crane can be linked with MES, ERP, real-time synchronization of operational data, which is also the key to unmanned workshop to achieve the full process automation.

    Core Technologies to Evaluate

    When selecting, the core technology directly determines the adaptability and stability of the crane, these five technical points must focus on, you can’t have one without the other.

    1. Intelligent Control System (PLC + AI)

    This is the “brain” of the intelligent bridge crane, the core is the combination of PLC control architecture and AI control algorithm, we often use Rockwell Control logix series PLC for integrated logic control and data processing, with Power Flex series inverter to realize the full digital vector control, the effect is more stable. Stable.

    It can realize motion control, AI task planning and automatic path optimization, and can complete the whole process of material gripping, handling and placing autonomously without human intervention.

    This system is especially critical for unmanned workshops with repeated production cycles and multi-station operations. For example, automotive parts workshop, repeat the same handling tasks every day, AI control algorithms can optimize the operation path, reduce ineffective action.

    The smart overhead crane system we made for an automobile factory is controlled by PLC+AI, realizing the automation linkage of multiple work stations and greatly reducing the waiting time.

    2. Anti-Sway Technology

    This is the necessary technology for unmanned operation, which is also the point that many purchasing managers tend to ignore. In the unmanned workshop, there is no operator to adjust manually, load swaying if uncontrollable, not only will delay the operation, but also may hit the equipment or materials.

    When selecting, we should focus on the active anti-sway control algorithm and load sway detection sensor, these two components directly determine the anti-sway effect.

    A good anti-sway intelligent crane can detect the magnitude of load shaking in real time, automatically adjust the crane’s operating speed and acceleration, quickly suppress shaking, and achieve faster positioning, but also reduce the stress on the crane structure, and extend the service life of the equipment.

    For example, long girder handling in steel structure factories, the load shaking amplitude is large, without advanced anti-shaking technology, it is impossible to realize unmanned operation, which is also our key consideration when selecting the model for steel structure factories.

    3. High-Precision Positioning

    Positioning accuracy directly affects the quality of operation, the requirements of different industries are not the same, the selection should be based on their own production needs, not blindly pursue high precision (the higher the precision, the higher the cost).

    Common positioning systems are laser positioning, absolute encoder, RFID markers and visual alignment, we will match according to the customer’s scene, such as precision workshop priority with laser positioning, heavy workshop with absolute encoder is more stable.

    Precision requirements of different industries, I organized a reference: automotive manufacturing needs ± 1-2mm, steel manufacturing ± 3-5mm, heavy manufacturing ± 5-10mm.

    Previously, an automotive parts customers, blindly choose the ± 1mm precision equipment, later found that it can not be used, but also spend a lot of cost, so it is important to accurately match the industry needs.

    4. Sensor & Safety System Integration

    In the unmanned workshop, safety is the bottom line, the sensor safety system must be complete, there can not be any omission. In our solutions for customers, we will build a triple protection network of “radar monitoring + video surveillance + interlock protection” to ensure operational safety.

    The core configuration includes load monitoring sensors, collision avoidance system, LiDAR/radar obstacle detection, emergency braking logic, as well as zoning and geo-fencing functions.

    Load monitoring sensors keep track of the loaded weight in real time to avoid overloading; anti-collision system prevents interference between multiple cranes; LiDAR/radar detects people or equipment intruding into the work area and immediately triggers emergency braking.

    These configurations are not optional, but are necessary to ensure the safe operation of unmanned workshop, the selection must be confirmed one by one, to avoid potential safety hazards in the later stage.

    5. MES / ERP / WMS Integration

    Without system integration, it is not a real intelligent bridge crane, and can not realize the whole process automation of unmanned workshop.

    The crane must be able to communicate smoothly with the MES (Manufacturing Execution System), ERP (Enterprise Resource Planning System) and WMS (Warehouse Management System) in the workshop to realize the real-time synchronization of operation data, such as the issuance of the handling task, the feedback of the operation status, and the recording of material information.

    Commonly used communication protocols are PROFINET, Ethernet/IP, OPC-UA, these protocols can be supported by our equipment, but also according to the customer’s existing system can be adapted, like Net Linx integrated architecture, to realize the integration of information, control and transmission.

    Previously, a customer bought an automated overhead crane that could not be interfaced with MES, and as a result, it still needed to issue tasks and record data manually, which did not realize real unmanned operation at all, and was equivalent to spending money for nothing.

    Key Technical Parameters for Selection

    In addition to the core technology, the matching of technical parameters is also very critical, directly affecting the service life of the crane and operational efficiency, these four parameters must focus on.

    Lifting Capacity & Span

    Selection, first of all, to match their own production workflow, such as the weight of the materials handled, the workshop’s span, can not blindly pursue large tonnage, large span.

    For example, heavy manufacturing workshop, need to handle dozens of tons or even hundreds of tons of materials, you need to choose a large-tonnage crane; and electronic components workshop, material weight is light, small tonnage will be enough.

    Also consider the future expansion needs, such as plans to expand the scale of production, increase the weight of materials, selection can be appropriate to set aside a certain margin, to avoid the late secondary replacement equipment, increase costs.

    When we make a plan for our customers, we will first calculate the actual needs of the workshop and future planning, and recommend the most suitable tonnage and span to avoid waste.

    Duty Classification

    This is the key to determine the durability of cranes, mainly referring to ISO 4301 and FEM classification (A5-A8), of which ISO 4301-5:2025 specifically for the classification of bridge and gantry cranes to make clear provisions.

    Unmanned heavy-duty workshop, because of the high intensity and long time of operation, usually need to choose a higher DUTY CLASS, such as A7, A8 class, so as to ensure the long-term stable operation of the equipment, and reduce the breakdown and shutdown.

    As for the unmanned workshop with small workload and long interval, it is enough to choose A5 or A6 class, which can meet the demand and save the cost.

    A heavy manufacturing customer chose A6 class equipment to save costs, but the result was that the parts were worn out in less than a year and had to be shut down for repairs, which delayed production.

    Speed & Acceleration Control

    The core is the Variable Frequency Drive (VFD), which can realize the smooth acceleration and deceleration of the crane, avoiding the load swaying due to excessive speed, and also reducing the mechanical wear of the equipment.

    At the same time, energy-saving motion curves are also important to reduce energy consumption, which can save a lot of electricity costs in the long run.

    Different industries have different needs, for example, automotive manufacturing workshops, where the work beat is fast and the running speed needs to be increased appropriately, and precision manufacturing workshops, where smooth running is required and the speed should not be too fast.

    Redundancy & Backup Systems

    An unmanned workshop cannot afford to have a “single point of failure”, otherwise the entire production process will be interrupted, so redundancy and backup systems are indispensable.

    The core configuration consists of a dual brake system, redundant control modules and emergency manual operators. The dual brake system avoids safety incidents caused by the failure of one brake; the redundant control module automatically switches to the backup module when the main module fails to ensure that the operation continues.

    Emergency manual operation device can manually intervene the crane operation in unexpected situations (such as power failure, system failure) to avoid material damage or equipment failure.

    Although this part of the configuration will increase the cost, but can greatly improve the reliability of the equipment, to avoid losses caused by downtime, for unmanned workshop is very important.

    Industry-Specific Considerations

    Unmanned workshops in different industries have different operating scenarios and pain points, and the selection cannot be generalized, but should be combined with industry-specific features.

    1. Steel Structure Plants

    The unmanned workshop in steel structure plants has three core pain points: long beams are shaking, multiple cranes are easy to interfere, and the welding line needs to be docked.

    When long beams are handled, the load shakes a lot, and ordinary anti-shaking technology can’t meet the demand, so it is necessary to choose anti-sway intelligent crane with advanced anti-shaking function to quickly suppress shaking and ensure operational safety.

    Multiple cranes operating at the same time, it is easy to collision interference, so you need to have a multi-crane coordination logic, to realize the partition automation, so that each crane in the designated area of operation, to avoid conflict.

    In addition, the crane should be able to seamlessly connect with the welding line to realize the automatic transfer and positioning of materials to match the production rhythm of the welding line and improve the overall efficiency.

    2. Automotive Manufacturing

    Automotive manufacturing workshop has a high degree of unmanned, the most stringent requirements for cranes, the core pain point is the production of fast beat, high positioning accuracy, the need for 24-hour uninterrupted operation.

    Positioning accuracy must reach ± 1-2mm to meet the needs of automotive parts handling and assembly, usually with laser positioning and vision alignment technology to ensure accurate positioning.

    At the same time, the crane must be able to integrate with the MES system in real time, receive production tasks, feedback operation status, with the workshop’s 24-hour production rhythm, there can not be any failure downtime.

    Redundant safety systems can not be missing, dual brakes, redundant control modules are necessary to ensure long-term stable operation of the equipment to avoid affecting the production rhythm.

    3. Heavy Manufacturing Workshops

    The core pain points of heavy manufacturing workshops are heavy loads, irregular workflow, high stress on equipment structure, and extremely high requirements on crane durability and adaptability.

    The duty class must be selected as high grade (M7-M8), and at the same time, the structure of the crane must be strengthened and designed to enhance the fatigue resistance to avoid damage to components caused by long-term heavy loads.

    The irregular operation flow requires the crane to have adaptive path planning function, which can adjust the handling path autonomously according to the material position and operation demand without manual intervention.

    In addition, the load monitoring sensors should be highly accurate, and can monitor the load weight in real time to avoid overloading and protect the equipment and material safety.

    Safety Standards &amp; Compliance

    Safety compliance is the bottom line for cranes in unmanned workshops, which must comply with relevant international standards and local regulations, otherwise they cannot be put into use and may face penalties.

    Commonly used standards include ISO 4301 (crane classification), FEM standards, CE certification, OSHA safety guidelines, and local industrial safety regulations, all of which will be confirmed one by one when we make solutions for our global customers.

    In particular, unmanned systems must have functional safety logic and redundant protection mechanisms, which are clearly required by international standards and are key to guaranteeing operational safety.

    For example, CE certification is a must for entering the European market. Our intelligent overhead crane for unmanned workshop can pass CE certification and meet the compliance requirements of European customers; for the North American market, it can also meet OSHA safety guidelines.

    When selecting a crane, be sure to check whether the equipment meets the standards of your region to avoid compliance issues that could affect production.

    ROI Considerations

    Many purchasing managers focus on the initial cost and ignore the long-term return on investment when selecting a model, which is actually a misunderstanding. The ROI of intelligent overhead cranes needs to be viewed from a long-term perspective, which is mainly reflected in these 4 aspects.

    Labor Cost Reduction

    One of the core advantages of the unmanned workshop is the reduction of labor costs. Traditional overhead cranes require a dedicated operator and supervision, making labor costs high.

    Intelligent overhead crane can realize fully automated operation, does not need full-time operator, only need a small number of maintenance personnel, can meet the daily operation requirements, greatly reducing labor expenses.

    For example, a medium-sized unmanned workshop, the original need for five crane operators, replaced by intelligent crane, only one maintenance personnel, can save hundreds of thousands of dollars a year in labor costs.

    Increased Productivity

    Intelligent cranes operate at a steady pace, without the fatigue and error problems of manual operation, and can realize 24-hour uninterrupted operation, significantly increasing productivity.

    Automatic anti-shaking and high-precision positioning can reduce the operating waiting time and speed up the operating rhythm; and the integration of MES system can realize the automatic issuance and scheduling of operating tasks to avoid ineffective action.

    We gave a steel structure customer to do the program, after replacing the intelligent crane, the workshop material handling efficiency increased by more than 30%, the overall production schedule has also accelerated a lot.

    Reduced Material Damage

    Manual operation is prone to positioning deviation and load shaking, resulting in material collision and damage, especially for precision parts, which can cause great loss after damage.

    Intelligent crane millimeter positioning and automatic anti-shaking technology, can accurately place the material, reduce collision, significantly reduce the material damage rate.

    For example, in the automotive parts workshop, the original manual operation of the material damage rate of about 5%, replaced by intelligent cranes, the damage rate dropped to less than 0.5%, which can save a lot of material costs a year.

    Typical Payback Period

    The payback period of different industries is different, mainly depends on the labor cost, work volume and material loss, I combined with our project experience, organized a reference:

    Automobile manufacturing: 2-4 years, this kind of workshop has high labor cost, large work volume, and the fastest payback;

    Steel fabrication: 3-5 years, moderate work volume, material loss reduction and labor cost savings is the main gain;

    Heavy manufacturing: 4-6 years, high initial investment, relatively stable work volume, slightly longer payback cycle, but long-term gains are obvious.

    Lifecycle Cost Analysis

    In addition to ROI, the full life cycle cost (TCO) of the crane should be accounted for, not only the initial purchase price, but also the long-term operating costs are critical.

    CAPEX Components

    Initial investment mainly includes 4 parts: crane hardware, automation system, software integration and commissioning costs.

    Crane hardware is the foundation, including main girder, end girder, hoisting mechanism, etc.; automation system includes PLC, AI control module, sensors, etc.; software integration is mainly the docking with MES and ERP system; commissioning costs are the debugging and trial operation after equipment installation.

    Many customers will choose low-cost automation system or software integration service to save cost, and as a result, the system is unstable and poor docking problems occur in the later stage, but increase the maintenance cost.

    OPEX Components

    Operating costs mainly include energy consumption, routine maintenance, software updates and predictive maintenance services.

    Intelligent cranes consume less energy than traditional cranes because variable frequency drives and energy-saving motion profiles can reduce power consumption; routine maintenance is mainly the inspection and replacement of sensors and braking systems; software updates can improve equipment performance and adapt to production upgrades in the workshop.

    Predictive maintenance service is very important, through the equipment operation data, to find potential faults in advance, to avoid downtime and reduce losses, which is also one of the value-added services provided by Henan Mine Crane to customers.

    Long-Term Value

    When selecting the model, we also need to consider the long-term value of the equipment, such as scalability, software upgradability and Industry 4.0 compatibility.

    Unmanned workshop upgrades quickly, cranes need to have scalability, according to the production needs to increase functionality or adjust the configuration; software upgradability allows the equipment to adapt to new production systems and technologies; Industry 4.0 compatibility, to ensure that the equipment is integrated into the factory’s intelligent ecosystem, will not be eliminated.

    Common Mistakes When Selecting an Intelligent Overhead Crane

    Over the years of serving global customers, I have seen many purchasing managers stepping on the pitfalls when selecting an Intelligent Overhead Crane, and I have summarized that these 5 mistakes are the most common and must be avoided.

    Think of automation as an add-on, not a system-level design. Many customers buy traditional cranes and then add automation modules, the result is that the system is incompatible, unstable operation problems, and can not realize the real unmanned.

    Ignore the network architecture. Intelligent cranes need stable network support in order to communicate smoothly with MES and ERP systems, many customers ignore the network construction, resulting in the equipment can not be linked properly.

    Underestimate the complexity of integration. System integration is not a simple docking, need to be combined with the workshop’s production process, the existing system for customization, many customers think that they can directly docking, the results of the late emergence of a variety of problems, delays in production.

    Choose low positioning accuracy equipment. In order to save costs, blindly choose low-precision equipment, the result can not meet the production requirements, had to be remodeled twice, but increased costs.

    No planning for future expansion. Selection only consider the current demand, no reserve margin, later expansion of production scale, the equipment can not be adapted, only to replace the new equipment.

    Selection Checklist for Procurement Managers

    In order to facilitate your quick check, I have compiled a procurement checklist, check against the selection, you can avoid most of the pits.

    1. clarify the required positioning accuracy, does it match your industry needs?

    2. cranes are compatible with existing MES systems, communication protocols match?

    3. is the safety redundancy system complete (dual brakes, redundant control modules, etc.)?

    4. Has the anti-shaking performance been tested and can it meet the demand of unmanned operation?

    5. Is the duty class aligned with the production output and can it meet the demand of long-term operation?

    6. Is there an upgrade path for the equipment to meet future production upgrades?

    Frequently Asked Questions

    Can existing overhead cranes be upgraded to intelligent systems?

    Yes, some of the upgrades are feasible, such as adding sensors and automation control modules to realize simple automation, just like the intelligent overhead cranes that many customers have chosen to upgrade, which can save a certain amount of cost.

    But if you want to achieve full unmanned, or new system integration is more efficient. Existing crane structure, control system may not be able to adapt to the complexity of the intelligent function, after the transformation of the stability and compatibility is not as good as the new equipment, in the long run, rather than directly purchasing a new intelligent overhead crane for unmanned workshop cost-effective.

    How reliable are unmanned crane systems?

    Unmanned crane systems are very reliable and even more stable than manual operation, provided they are equipped with redundant controls and predictive maintenance.

    The equipment we provide to our customers around the world reduces the risk of a single point of failure through dual braking and redundant control modules; predictive maintenance services can identify potential failures in advance to avoid downtime. Many of our customers have equipment that operates 24/7 with an annual failure rate of less than 3%.

    What is the ideal positioning accuracy?

    There is no uniform standard, the key is to look at the needs of the industry. Accuracy requirements vary greatly from industry to industry, and the core is to match your own production needs.

    Automobile manufacturing needs the highest accuracy, usually ± 1-2mm; steel structure manufacturing ± 3-5mm can be; heavy manufacturing ± 5-10mm is enough, blind pursuit of high accuracy will only increase the cost, no practical significance.

    Is intelligent crane suitable for heavy-duty loads?

    As long as you choose the right duty class and strengthen the structure design, it can meet the demand of heavy-duty loads.

    The intelligent overhead crane we provide to our heavy-duty manufacturing customers has a duty class of A8 and a reinforced structure that can handle hundreds of tons of loads, and at the same time automate operations to meet the needs of unmanned workshops.

    Conclusion

    The core of choosing intelligent overhead crane for unmanned workshop is not to pursue the gimmick of “intelligent”, but to choose a complete system that can really fit your workshop and solve the actual pain points.

    It needs to have reliable core technology (PLC+AI control, automatic anti-shaking, high-precision positioning, etc.), match the technical parameters of the industry needs, meet international safety standards, and at the same time can be seamlessly integrated with the workshop’s production system.

    When selecting a model, you can’t just look at the initial cost, but also account for the long-term ROI and full life cycle cost, avoid those common pits, and take into account the current demand and future expansion.

    Henan Mine Crane Factory Custom

    Henan Mine Crane has done more than twenty years of crane R & D and production, to provide unmanned workshop crane solution to the global unmanned workshop in many industries, familiar with the pain points and needs of different industries.

    We will not simply recommend equipment to you, but will customize the most suitable solution according to your workshop scenarios, production needs, budget, to help you achieve truly unmanned operations, improve productivity and reduce long-term costs.

    Whether you are a new unmanned workshop, or existing workshop upgrade, you can contact our engineering team, we will give you a free demand estimation and program planning, to help you choose the right equipment, less detour.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose an Intelligent Crane for Unmanned Workshop?

    How to Choose an Intelligent Crane for Unmanned Workshop?

    How to Choose an Intelligent Crane for Unmanned Workshop?

    Unmanned workshop is the core of manufacturing enterprises to reduce costs and increase efficiency and realize intelligent transformation. Intelligent crane directly determines the level of automation, productivity and operational safety of unmanned workshop, many enterprises fall into the parameter stacking, blind pursuit of high-end misunderstanding, resulting in a disconnect between equipment and demand. Combined with the latest technology trends in 2026 and thousands of landing cases, from a multi-dimensional guidance to enterprises to select the right intelligent crane for unmanned workshop, to help realize unmanned production.

    What Is an Intelligent Crane?

    Definition of intelligent crane system

    Intelligent crane integration of automation control, sensor positioning, data communications and other areas of technology, can autonomously complete the material grasping, handling, positioning, scheduling, sensing and analysis of decision-making and implementation of closed-loop, and unmanned workshop with other systems to collaborate with the linkage, is the core component of the unmanned crane solution, is not a simple automation and crane superimposed.

    Difference between traditional crane and intelligent crane

    Traditional cranes are operated manually as the core, relying on the operator’s experience and judgment, there are problems such as low efficiency, large errors, and many safety hazards. The intelligent crane completely get rid of artificial dependence.

    • Operation mode: Traditional cranes need to be operated on-site, intelligent cranes can realize fully autonomous operation, remote monitoring, without human intervention.
    • Precision control: Traditional crane positioning error in centimeters, intelligent cranes can achieve millimeter-level positioning, suitable for precision material handling needs.
    • Synergy: Traditional cranes run independently and cannot be linked with other systems in the workshop. Intelligent cranes can be seamlessly connected to the MES, ERP system, to achieve global scheduling.
    • Safety: Traditional cranes rely on manual warning, intelligent cranes with active anti-collision, real-time status monitoring and other functions, to avoid safety risks from the source.
    • Operation and maintenance mode: Traditional cranes use after-the-fact maintenance, intelligent cranes support predictive maintenance, early warning failures, reduce downtime losses.

    Key technologies involved

    Intelligent crane intelligence, is dependent on the synergistic support of the four core technologies.

    • Automation control system: PLC as the core, equivalent to the core control unit of the intelligent crane, can independently plan the handling path, adjust the operating speed, to achieve unmanned operation, is the core of the automated crane system.
    • Sensor and positioning system: Laser positioning, visual positioning, encoder and other technologies, combined with MEMS acceleration sensors and fiber grating strain sensors to achieve millimeter-level accurate positioning, real-time sensing of the location of the material, the state of the equipment, to ensure the accuracy and safety of the handling, is the key to intelligent material handling.
    • Data communication and remote monitoring: Through industrial Ethernet, 5G and other high-speed communication protocols, real-time data interaction between the equipment and the workshop control system and remote monitoring platform can be realized, supporting remote scheduling, troubleshooting, and data visualization, and some of the high-end models support 5GVR remote control, which effectively improves the efficiency of operation and maintenance.

    Why Intelligent Cranes Are Essential for Unmanned Workshops

    Intelligent cranes are essential for unmanned workshops, and their necessity is directly related to the productivity, operating costs and market competitiveness of enterprises. Combined with the thousands of unmanned workshop cases we have served, the core advantages are as follows.

    Reduce labor dependency

    The core demand of unmanned workshop is unmanned, traditional cranes need to be equipped with professional operators, and there are recruitment difficulties, high training costs, personnel mobility and other issues. Intelligent cranes can realize fully autonomous operation, without the need for on-site operators, only 1-2 remote monitoring personnel can manage multiple devices, significantly reducing labor costs, cracking the unmanned workshop labor shortage problem.

    Improve operation efficiency and consistency

    Manual operation has low efficiency, easy to fatigue, error and other problems, intelligent crane can be in accordance with the preset program, accurate completion of handling, positioning and other operations, no fatigue, no error, operational efficiency than traditional cranes to enhance more than 30%, and can ensure the consistency of handling, suitable for precision manufacturing, mass production of unmanned workshop. Statistics show that it can increase the material handling efficiency of traditional workshop by more than 300%, significantly improving the comprehensive efficiency of the equipment.

    Enable continuous 24 hour operation

    The advantage of unmanned workshop is all-weather production, traditional cranes are subject to artificial rest, shift and other restrictions, can not realize 24-hour operation. Intelligent cranes do not need to rest, can be continuously operated around the clock, combined with intelligent scheduling system to reasonably allocate handling tasks, maximize the release of unmanned workshop capacity, suitable for large orders, fast-paced production enterprises.

    Enhance safety in high risk environments

    Many unmanned workshops have high risk environments such as high temperature, high pressure, toxicity, radiation, etc., and the risk of manual operation is extremely high. Intelligent cranes can realize remote control, autonomous operation, the operator does not need to enter the high-risk areas, from the source to avoid safety risks, while equipped with anti-collision, overload protection, emergency braking and other multiple safety mechanisms, so that the crane accident rate dropped by more than 80%.

    Support smart factory transformation

    As the core equipment of the unmanned workshop, the smart crane can be seamlessly connected with MES, ERP, WMS and other systems to realize the digital management of material handling, production scheduling, equipment operation and maintenance, and provide core support for smart factory transformation. Through real-time collection of equipment operation and handling data, it helps enterprises optimize the production process, accurately control costs, and promotes enterprises to upgrade from automation to intelligence, which is in line with the national development trend of intelligent manufacturing.

    Main Types of Intelligent Cranes for Automated Workshops

    Different types of intelligent cranes, applicable scenarios, operational capacity differences, the first step in the selection is to match the scene, combined with the layout of the unmanned workshop, material type, operational requirements, the following three are the most commonly used types, covering more than 90% of the unmanned workshop scenarios.

    Intelligent Overhead Crane

    Intelligent Overhead Crane is the main equipment of indoor production line in unmanned workshop, suitable for indoor production workshop and precision manufacturing workshop, with compact structure and small space occupation, which won’t affect the operation of the ground equipment, with high positioning accuracy, which can be customized according to the workshop’s span and height, and suitable for the handling needs of materials of different weights, and part of the model adopts the design of low headroom, which can enhance the vertical operation space.

    Intelligent Gantry Crane

    Intelligent gantry cranes are suitable for large unmanned workshops and outdoor work areas, and are the preferred equipment for heavy-duty scenarios in industrial automation cranes. They can be deployed independently without the need to rely on the roof of the workshop, and have a strong loading capacity, which is suitable for the handling of heavy materials and large parts, and have a high level of protection, which can withstand the harsh outdoor environment, and support all-weather continuous operation, and are suitable for all kinds of heavy-duty work conditions.

    Automated Handling Crane System

    Automated Handling Crane System is an integrated form of unmanned crane solution, mainly applicable to unmanned warehouses and logistics sorting workshops, can be seamlessly connected to the warehouse automation system to realize the full automation of material inbound, outbound, inventory and sorting, which can enhance the utilization rate of the warehouse space, and support the collaborative operation of multiple devices to enhance the logistics handling efficiency.

    Key Factors When Choosing an Intelligent Crane

    The core of selecting an Intelligent Crane is to match the actual needs, without blindly pursuing high-end configuration. A number of key factors directly determine the practicality, stability and input-output ratio of the equipment, these factors need to be combined with the actual working conditions of the unmanned workshop to focus on the investigation, a reasonable balance of indicators, in order to select the appropriate equipment.

    Automation level

    The automation level of intelligent cranes is divided into two categories: semi-automatic and fully automatic. When selecting cranes, it is necessary to combine the automation level of unmanned workshops and production requirements to avoid under- or over-configuration, and at the same time, it is necessary to anticipate the future production plan to ensure that the selected equipment can be adapted to the workshop to meet the subsequent upgrading requirements, and to ensure the long-term usability.

    Positioning accuracy

    Unmanned workshop material handling requires high positioning accuracy, positioning error will lead to material damage and production interruptions, the selection of intelligent cranes need to focus on positioning accuracy indicators, combined with the type of material to determine the appropriate accuracy standards, while understanding the adaptability of commonly used positioning technology to protect the handling accuracy and operational safety.

    Anti sway performance

    Anti-swing performance is crucial for intelligent cranes, especially in high altitude and heavy load handling scenarios, as the swaying of the spreader will affect the operational efficiency and safety of intelligent cranes. When selecting cranes, attention should be paid to the control algorithm of the equipment. High-quality equipment can effectively control the swaying amplitude of the spreader to ensure that there is no obvious swaying during lifting and operation to ensure operational safety and handling efficiency, which is suitable for all kinds of unmanned workshop working conditions.

    Load capacity and duty class

    Load capacity and duty class are the basic indexes of intelligent cranes. When selecting cranes, it is necessary to combine them with the operating conditions of unmanned workshops, determine the load capacity according to the maximum weight of materials to be handled on a daily basis, and at the same time, leave a reasonable margin, and select the appropriate duty class in combination with the frequency of operation and the demand for continuous operation, so as to avoid insufficient loading or wastage of resources.

    System integration ability

    System integration ability is the key to the intelligent crane to play the advantages of intelligence, the selection of intelligent cranes need to confirm that the equipment can be seamlessly connected with the existing system of unmanned workshop to achieve synchronization of production scheduling, material information and inventory data, to ensure that the production and handling of synergies, to avoid the later compatibility issues to increase the cost of transformation.

    Safety design

    Unmanned workshop without artificial on-site supervision, the safety design of the intelligent crane is particularly important, choose the right intelligent crane need to pay attention to anti-collision, overload protection, power failure protection and emergency stop and other functions, while confirming that the equipment has the ability to monitor the real-time operating status, can be an early warning of failures, to avoid safety accidents and interruptions in production.

    Remote monitoring and control

    Remote monitoring and control functions can reduce the cost of unmanned workshop equipment operation and maintenance, selecting intelligent cranes need to pay attention to whether the equipment supports remote centralized scheduling, operation data visualization and handling trajectory traceability, and at the same time, confirm that the remote troubleshooting and parameter debugging capabilities, reduce the input of on-site operation and maintenance personnel to enhance the management efficiency.

    Maintenance and reliability

    The reliability of equipment directly affects the continuous production of unmanned workshop, when selecting the equipment, we need to examine the predictive maintenance ability, the quality of core components and after-sales service, to confirm that the supply of spare parts is sufficient to provide timely maintenance support, while paying attention to the material and process of the equipment, to ensure that the equipment has a low failure rate and a long service life, and to reduce the unplanned downtime.

    Typical Application Scenarios

    Unmanned workshop in different industries, material types, operational needs vary greatly, the following are five typical application scenarios, you can benchmark your own industry, quickly lock the selection direction.

    1. Material handling in steel mills: With heavy load, high temperature and continuous operation as the core demand, intelligent gantry cranes are preferred, requiring strong load capacity, high protection level, high temperature prevention, fully automated handling of billets and steel, and part of the scenarios need to be equipped with multi-modal data fusion safety assessment system.
    2. Automated Warehouse: With high efficiency, precision and synergy as the core demand, the automated handling crane system is preferred, which needs to have the ability to integrate with WMS and AGV systems, support multi-storey shelves and dense storage of materials handling, and realize efficient connection between warehouse and production line without connection fault.
    3. Manufacturing production line: With precision, flexibility and high efficiency as the core demand, intelligent overhead travelling crane is preferred, which is required to have high positioning accuracy and good anti-swinging performance, adapt to the precision material transfer between processes, and be able to collaborate with the MES system to synchronize the production beats.
    4. Paper and pulp industry: With wet, heavy load as the core demand, give priority to intelligent cranes with high protection level and corrosion resistance, requiring stable load capacity, automated handling of paper rolls and pulp, and anti-corrosion process for key components.
    5. Port and yard operations: Outdoor, heavy-duty, all-weather operations as the core demand, giving priority to intelligent gantry cranes, requiring strong adaptability, wind resistance, can realize the fully automated handling of containers, large cargo, some models have blockchain equipment traceability.

    Common Mistakes to Avoid

    Combined with our years of experience in selection services, many companies in the selection of intelligent cranes, easy to fall into the following four misunderstandings, resulting in equipment that can not be adapted to the needs of the waste of inputs, must be avoided.

    • Choosing low automation level for future needs: Some enterprises choose intelligent cranes with low automation level to save costs, which leads to unmanned workshop upgrading in the later stage, the equipment can not be adapted to the need for replacement, but increase costs.
    • Ignoring system compatibility: In advance to confirm the compatibility of the crane with the workshop existing MES, ERP and other systems, resulting in the installation of the equipment can not be integrated, can not realize intelligent collaboration, reduced to automation crane.
    • Focusing only on price: Some companies choose low-priced equipment, it seems to save the initial cost, but the equipment failure rate is high, high maintenance costs, lagging after-sales service, instead of affecting the production, increasing long-term costs, technological sophistication is not blindly stacked high-end configuration, need to be combined with the actual scenario match.
    • Overlooking after sales service: The operation and maintenance of intelligent cranes require professional technical support, some companies choose the manufacturer of imperfect after-sales service, equipment failure can not be repaired in a timely manner, resulting in production interruptions, causing huge losses.

    Future Development Trends

    With the continued promotion of Industry 4.0, the technology of intelligent cranes is constantly upgraded, combined with the latest technology trends in 2026, the future will be developed in the following four directions, the selection can be properly pre-judged, choose the equipment with the potential for upgrading.

    • Fully autonomous crane system: Without human intervention, it can realize autonomous path planning, material identification, fault self-healing, and even work with robots to achieve truly unmanned handling.
    • Deep integration with smart factory: Not only material handling equipment, but also will become the data node of the smart factory, which can collect and analyze data in real time to provide more accurate support for production scheduling and process optimization, and combine with digital twin technology to realize real-time mapping and interaction between the virtual and real worlds.
    • Upgrade of digital monitoring platform: The use of big data, artificial intelligence technology, to achieve accurate prediction of the operating state of the equipment, fault warning, and even the integration of remote operation and maintenance and predictive maintenance can be realized, and multiple cranes working together will show more advanced group intelligence.
    • Popularization of energy-saving technology: The use of energy-saving motors, energy feedback systems and other technologies to reduce equipment energy consumption, combined with reinforcement learning load balancing algorithms, dynamic adjustment of operating parameters, reducing energy consumption by more than 15%, to help enterprises realize green production, the future may appear zero-carbon cranes, relying entirely on renewable energy operation.

    Henan Mine Crane Factory Custom

    As a large-scale intelligent crane manufacturer in China, Henan Mine Crane Factory can provide one-stop unmanned crane solution from customized design, equipment supply, system integration to after-sales service, to help enterprises achieve unmanned production upgrade, reduce costs and improve efficiency.

    The selection of intelligent cranes is not about parameterization, but long-term value. Choose a suitable demand, reliable quality, perfect service intelligent crane, in order to escort the efficient operation of unmanned workshop, to achieve the long-term goal of intelligent transformation of enterprises.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose an Electromagnetic Crane for Automated Metal Handling?

    How to Choose an Electromagnetic Crane for Automated Metal Handling?

    How to Choose an Electromagnetic Crane for Automated Metal Handling?

    Steel mills, scrap yards, metal fabricators are always pushing harder to get more material through quicker, with less experience on the shop floor. The answer is automation, and the electromagnetic crane is the component that allows automated ferrous metal handling to happen at all.  However if you get the spec wrong this will end up being a crane that can‘t keep pace with your line, drops material where it shouldn‘t or refuses to communicate with your automation system.

    What‘s an electromagnetic crane, why is it the backbone of automated metal handling, and 10 factors that REALLY influence if a crane will be successful in your facility are covered in this guide.  Where you should go wrong when buying a crane,  questions to ask a supplier before buying a quote, and where you should customize are in here too.

    What Is an Electromagnetic Crane?

    An electromagnetic crane is an overhead or gantry crane that has an electromagnetic lifting head as opposed to the usual hook, sling, grab, etc.  The magnet has a coil through which you send direct current; the resulting magnetic field has enough pull to hold ferrous material. Remove the current and the magnetic field collapses and you drop whatever you had clamped. That simplicity is an advantage when automating repetitive operations,  such as separation.

    A complete system has four main components:

    • Electromagnetic lifting chuck: It is a supporting operation device at the lower end of the hook, which can directly contact and absorb various loads. It is the core executive component to realize material grabbing operation.
    • Bridge/gantry crane: composed of bridge, hoist and walking trolley, mainly used to accurately adjust the operation position of electromagnetic chuck, complete the translation, alignment and positioning of load.
    • Control system: the core function is to control the excitation and demagnetization of electromagnet, and at the same time, it can coordinate the whole set of control logic of equipment operation and accurate positioning under automatic working conditions.
    • Power supply and cable reel device: stable supply of DC power for the electromagnetic chuck moving dynamically throughout the whole process, accurate control of current transmission status, to ensure continuous power supply and reliable operation during dynamic operation of the equipment.

    This, compared to a mechanical grab crane,  is the contact and control. A grab crane is a grab against a load with hydraulic or mechanical jaws, requires force and is slow and imprecise, an electromagnetic is an instant grip across a wide, even contact zone and as quick to release, however, only works on ferrous metal and load release is wholly dependent on power quality.

    Why Electromagnetic Cranes Are Ideal for Automated Metal Handling

    Increased Productivity

    Since the magnet engages and releases in less than a second automated electromagnetic cranes significantly reduce cycle time when compared to the slower, manually rigged slings or grabs.  When incorporated into a controlled sequence such a crane can operate non-stop loading,  conveying and stacking product without operator intervention feeding upstream and downstream processes at a consistent rate.

    Improved Workplace Safety

    Automation also removes operators away from suspended loads and away from hot or sharp or unstable material. A properly specified magnet will also hold more securely and evenly than a man-handedly rigged sling,  again allowing a more controlled transportation and less risk of load movement or dropping provided the magnet is properly sized and supported by the safety systems discussed later in this guide.

    Lower Operating Costs

    Less manual rigging steps means less man hour cost per lift. Even,  hands-off contact lessens surface damage to plate & coil products which can be important where material finish has greater eventual resale or downstream processing value.  Ultimately, the speed,  less damage and less staffing help justify the added cost of an automated electromagnetic crane.

    Key Factors to Consider When Choosing an Electromagnetic Crane

    Type of Material to Be Handled

    Choosing a magnet begins by considering the workpiece; what you are lifting are steel plates, billets, scrap, coils,  pipe, beams, rebar, pig iron, ore? The shape of the workpiece determines the shape of the magnet.

    Regular, flat workpieces like plates, coils and slabs require large,  flush,  even contact points rectangular or square magnets are ideal in this application.  Dodge irregular or loosely piled loads, such as mixed scrap or cast ingots by using a circular magnet that extends into the spaces and clutches uneven surfaces. Rectangular or square magnets are suitable for long,  round materials such as coiled rebar or pipe.

    Material Weight and Load Capacity

    Define capacity in terms of three figures: the maximum single load you expect to lift, an average load per shift, plus a safety margin above each. Under-sizing leads to a limit and a safety problem; over-sizing leads to capital sitting idle on capacity you never need. Allow for growth in planned production levels if higher capacity is needed it is much easier to add an extra gear or two later than upgrade the crane structure.

    Material Typical Unit Weight Recommended Crane Capacity
    Steel plate (single sheet) 1–15 tons 5–20 tons
    Steel billet (bundle) 2–10 tons 10–20 tons
    Scrap steel (mixed pile) 0.5–5 tons per lift 5–15 tons
    Steel coil 5–25 tons 15–32 tons
    Pig iron / ingots 0.5–2 tons per lift 5–10 tons

    Figures are general planning ranges, always confirm exact load data with your crane supplier before finalizing capacity.

    Material Temperature

    Cold-rolled and ambient temperature material can run on standard (room-temperature) magnets. Hot steels direct from the rolling mill or furnace require special high-temperature electromagnets using heatable coil insulation and materials rated for sustained operation far above ambient. These magnets will usually require forced-air or even water cooling to run in a safe coil temperature range and to prevent early coil insulation destruction. If you have any portion of your process that handles hot material, temperature rating is not and should not be optional: it is the first filter step for your magnet choices.

    Lifting Frequency and Duty Cycle

    Duty cycle is the percent of time the magnet can remain energized safely within a constant cycle (often 10-minute, generally) without over-heating.For example, a magnet rated at 60% duty cycle can operate energized for 6 minutes of 10 minutes without overheating.

    Heavy-duty, high frequency assembly lines in manufacturing require magnets rated for higher duty cycles some high frequency designs operate 75% or more while intermittent, lower-volume operations can operate using standard duty magnets at a lower cost.The crane duty rating (see safety section below) should be relative to the operation frequency, not only the peak lifting capacity.

    Automation Compatibility

    An electromagnetic crane bought for automated handling has to function as one node in a larger control system, not a standalone machine. Confirm the crane and its control system can integrate with:

    • Industrial robot: It can carry out parallel cooperative operation with cranes, and can undertake the connection and supporting processing tasks of upstream and downstream processes.Through signal interaction, equipment linkage interlocking is realized to avoid action conflict and meet the continuous automation operation requirements of assembly line.
    • MES and ERP management platform: It can collect and monitor on-site inventory and material flow data in real time, and dynamically update the production and operation status of the whole line.Relying on data linkage, closed-loop management of production planning, material scheduling and warehousing information is realized, and fine control of factories is supported.
    • Automatic production line: strict synchronization and coordination requirements for equipment action sequence, operation rhythm and start-stop logic.Electromagnetic crane shall match the overall rhythm of production line to complete synchronous start and stop and accurate alignment, so as to ensure continuous and stable operation of the whole line.
    • Remote monitoring system: Support operators to complete remote monitoring, status viewing and fault warning of multiple cranes in the central control room.It can realize centralized and unified dispatching of equipment and remote start-stop control, greatly reduce on-site duty intensity and improve operation and maintenance efficiency.
    • Smart Factory and Industry 4.0 Infrastructure: Complete data acquisition, log storage, status archiving, and intelligent analytics capabilities.It can upload equipment operation parameters, operation records and fault data in real time, providing data support for equipment operation and maintenance, capacity optimization and digital upgrading.

    If the electromagnetic crane can not communicate with the existing industrial system to achieve control signals and data interaction, it will form an automatic island.Even if the peripheral equipment has been fully automated, the equipment still needs to rely on manual trigger operation, which seriously restricts the automation level and production efficiency of the whole production line.

    Magnet Type Selection

    Magnet Type Best Suited For Key Characteristic
    Circular lifting magnet Scrap, ingots, irregular piles Even field spread; grips loose, uneven material
    Rectangular/plate magnet Steel plate, slab, sheet Flat, concentrated contact for regular surfaces
    Billet lifting magnet Billets, blooms, square/round bar Deep-penetration field for stacked or bundled bar stock
    Coil lifting magnet Steel coil Vertical, horizontal, or dual-orientation lift
    Scrap handling magnet Mixed ferrous scrap High penetration depth to reach material below the surface pile

    Other suppliers can provide magnet beams, a row of magnets mounted along a spreader to lift multiple items or spread magnetic force across a long load. First match the type of magnet to the main material, then confirm it is rated for the secondary materials; don‘t assume one magnet does the full job.

    Power Supply Requirements

    Electromagnetic cranes use DC power to drive work, so the whole system must be equipped with rectifier devices to convert the AC power into DC power available to the equipment.In the process of power supply system selection and configuration, it is necessary to focus on the following core indicators and functional design:

    • Power-off protection and standby power supply system: battery backup power supply or equivalent power-off protection device shall be equipped to construct reliable emergency power supply guarantee mechanism.This configuration can continuously supply power when the main power supply is interrupted suddenly, effectively prevent the material from falling during the lifting process, and avoid major safety accidents.
    • Rectifier specification matching electromagnet peak current:rectifier selection needs to be matched according to the peak current of electromagnetic chuck, not only refer to the average working current.This can meet the large current demand of the equipment for instantaneous absorption, avoid overload failure, and ensure stable operation of the crane under full load conditions.
    • Energy-saving operation function configuration: electromagnetic chuck long-term load operation will continue to consume current, energy consumption accumulated loss is large.The system shall be equipped with energy-saving regulation function, which can optimize current output under stable load maintenance condition and effectively reduce energy consumption cost of equipment for long-term operation.

    The stability of power supply is not only related to the operation efficiency of equipment, but also the core safety guarantee of electromagnetic crane operation.The fixing reliability of electromagnetic chuck depends entirely on the stability of power supply system. Stable and reliable power supply system is the core premise of safe operation of equipment.

    Working Environment

    Indoor and outdoor applications have different requirements.  If the HMI is outdoors,  look for something protected from rain and dampness while also resistant to corrosion. In dusty environments sealed enclosures are crucial to prevent dust from the coil or control cabinet.  Environments at high temperature also add to the cooling needs we‘ve already mentioned.  Finally, if there is a chance your operation will be considered an explosive environment ,  explosion-protected electrical components are needed to be declared with the vendor.

    Crane Structure

    Structure Advantages Best Suited For
    Single-girder overhead crane Lower cost, lighter structure Lighter loads, smaller spans
    Double-girder overhead crane Higher capacity, greater stability Heavy, high-frequency magnetic lifting
    Gantry crane Doesn’t require overhead runway; works outdoors Yards, ports, outdoor storage
    Semi-gantry crane Combines runway-mounted and floor-supported legs Facilities with partial building coverage

    A gantry crane is helpful, comparable in a way to the double-girder to achieve the extra stability and margin of capacity often needed. Gantry or semi-gantry overhead cranes are though ideally used in outside yards where an overhead run way is not cost-appropriate or feasible.

    Safety Features

    Automatic electromagnetic crane relies on magnetic field to absorb tons of iron materials, and the safety of operation highly depends on magnetic stability.Therefore, the safety system must preset the risk of magnetic field failure, supporting multiple protection mechanisms, and the specific safety configuration requirements are as follows:

    • Standby battery power supply system: able to maintain electromagnetic adsorption force continuously under instantaneous power failure conditions, effectively prevent falling materials in the air, and ensure the safety and stability of automatic operations.
    • Magnetic real-time monitoring function: real-time acquisition and monitoring of suction disc adsorption magnetic parameters, once the load holding magnetic force is lower than the safety threshold immediately trigger early warning, avoid the risk of loss of load caused by magnetic attenuation in advance.
    • Load real-time display device: real-time detection and visual display of the actual weight of the lifting material, accurate check of the operating load, to ensure that the whole process in the equipment rated safe load range.
    • Overload protection mechanism: equipped with intelligent overload protection logic, it can automatically limit over-limit lifting behavior, strictly prohibit operation beyond rated load, and eliminate equipment failure and safety accident caused by overload from the root cause.
    • Emergency stop device: Considering the field operators and automatic control scenarios, equipped with convenient emergency stop trigger channel, it can quickly stop under sudden abnormal conditions and terminate dangerous operations in time.
    • Anti-swing control technology: through dynamic algorithm to suppress the swing deviation in the process of material lifting, effectively improve the stability, accuracy and operation efficiency of automatic handling.
    • Travel limit switch: accurately restrict the operation travel and lifting height of the crane, effectively avoid over-hoisting, over-travel and other illegal actions, avoid equipment structure collision and mechanical damage.
    • Remote fault diagnosis function: support real-time online monitoring and data analysis of equipment operation status, predict potential faults in advance, realize fault pre-treatment, and reduce the risk of equipment shutdown and sudden failure.

    Common Mistakes When Selecting an Electromagnetic Crane

    In the selection process of automatic electromagnetic crane and electromagnetic chuck, most of the problems such as equipment failure, low efficiency and high cost of transformation originate from unreasonable decision-making in the selection stage.The following are the most common mistakes in the industry:

    • Price alone as the selection criteria: blindly choose low-cost equipment, will lead to electromagnetic chuck specifications are too small, the working load rate is not up to standard, can not adapt to the actual working conditions
    • Neglecting the working cycle adaptation requirements: not matching the equipment load duration according to the working condition standard, it is easy to cause problems such as overheating of the chuck and unplanned shutdown of the equipment, which greatly shortens the service life of the electromagnetic chuck.
    • Underestimating future production expansion demand: only referring to the current production capacity selection, without reserving equipment performance margin, the equipment cannot meet the demand for production increase after several years of use, and is forced to invest high costs for equipment upgrading and transformation.
    • Electromagnetic chuck type selection error: different structures of electromagnetic chuck adapt to the type of material there are differences, adapt to the plate lifting chuck can not efficiently grab loose waste, and vice versa, mismatch will directly lead to a significant decline in operating efficiency.
    • Ignoring automation compatibility performance: The system integration capability of the equipment is not considered when selecting, resulting in the crane being unable to interface with the factory automation control system, and the subsequent high cost of equipment modification is required to achieve intelligent linkage.
    • Disregard the convenience of equipment operation and maintenance: The selection of electromagnetic chuck and control system with great difficulty in maintenance and maintenance will significantly increase the difficulty of daily operation and maintenance of equipment and increase the long-term operation cost of production line.
    • Neglecting the environmental conditions of the site working conditions: failure to select equipment with corresponding protection level according to outdoor, high temperature, corrosion and other special working conditions will lead to accelerated aging of the electromagnetic chuck, premature failure, and greatly reduced stability and service life of the equipment.

    Maintenance Considerations Before Purchasing

    • Routine Inspection: Ongoing reliability depends on regular checks of the magnet surface for wear or damage, electrical cables for insulation breakdown, brake systems for wear, and control panels for fault codes or loose connections.
    • Preventive Maintenance: A sound maintenance program includes periodic coil resistance testing , power supply inspection, mechanical lubrication of crane moving parts, and regular verification of every safety system listed above.
    • Expected Service Life: Magnet and crane service life depends on operating hours, load frequency, environmental conditions, and the quality and consistency of maintenance. Ask any supplier for realistic service-life expectations under your specific operating profile, not just a generic figure.

    Conclusion

    Electromagnetic crane selection not only depends on lifting tonnage, but also needs to integrate multiple indicators such as material characteristics, operation frequency, automation adaptation, safety protection and operation and maintenance to ensure efficient and stable operation of the system.There is no general selection standard for different plant conditions. Equipment schemes can be customized according to actual parameters on site, which can effectively reduce costs and improve efficiency and realize safe standardized operation.

    Henan Mine Crane focus on heavy lifting field, can provide steel, metal processing, waste recycling and other industries with a full range of lifting equipment and intelligent customized solutions.We provide working condition analysis, automation integration, customized design and full-process technical support to help customers improve production safety, efficiency and equipment operation stability.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose a Suitable Grab Bridge Crane for a Waste Treatment Plant

    How to Choose a Suitable Grab Bridge Crane for a Waste Treatment Plant

    How to Choose a Suitable Grab Bridge Crane for a Waste Treatment Plant

    Grab bridge cranes are not simple handling tools in a waste treatment plant. Whether it is feeding and sorting in a domestic waste incineration plant, or transferring and stockpiling at a waste transfer station, it is indispensable in every core process.

    Especially in the waste incineration power generation project, the crane is responsible for the rubbish accurately into the incinerator, but also with the completion of the rubbish mixing and stirring, and its operating status directly affects the efficiency of incineration – if the feed is not uniform, there will be insufficient combustion, furnace temperature fluctuations, which affects the efficiency of power generation and environmental emissions.

    Grab Type Bridge Crane

    Grab Type Bridge Crane

    More critically, once the crane selection is not appropriate, the subsequent trouble will continue to flow: frequent breakdowns and shutdowns, resulting in the accumulation of rubbish, interruption of the production line; maintenance costs remain high, and a year of maintenance costs can even catch up with the difference in the price of the equipment itself;

    Serious cases will also affect the incineration stability, today combined with years of experience in the industry, to talk to you about how to choose to avoid these pits, selected to fit and durable equipment.

    First understand the operating conditions of the waste treatment plant

    Let’s choose the type, do not rush to see the parameters of the equipment, you have to first feel through the operating environment of their own plant – waste treatment plant conditions and ordinary factories are not the same, continuous operation, harsh environments, variable loads, these characteristics directly determines the configuration of the crane requirements.

    Continuous operation of the mandatory requirements

    Many waste treatment plants, especially waste incineration power generation projects, are running 24 hours a day, cranes must also follow the continuous rotation, can not have a long time downtime.

    This requires that the equipment must reach the heavy-duty operation level, that is, the industry said FEM A7/A8 level, or CMAA E/F level, in short, can withstand high-frequency start and stop, continuous heavy-duty operation, will not fail because of long-time operation.

    We can understand this way, ordinary factory cranes may only run for a few hours a day, while the cranes in rubbish factories, 24 hours a day, there may be 20 hours in the repeated grabbing, transferring rubbish, the motor, transmission, brake loss is extremely large, light load level of equipment can not carry.

    Harsh operating environment

    How harsh the environment of the rubbish treatment plant, have done the operation and maintenance of friends are clear, this is also easy to wear and tear of the crane core reasons.

    First of all, high humidity, rubbish pit, sorting workshop is always in a humid state, especially in summer, the water vapour in the air mixed with the steam from the rubbish leachate, it is easy to erode the metal parts of the equipment; secondly, corrosive gases, fermentation of rubbish will produce hydrogen sulphide, ammonia and other corrosive gases, these gases will slowly corrode the main beams, electrical cabinets and cables, and after a long time, there will be rusty parts, electrical short-circuit problems.

    Coupled with the high dust and odour in the workshop, the dust will drill into the cracks of the motor and gearbox, wear the internal parts, and will also block the electrical interface, further increasing the probability of failure. So when we select, anti-corrosion, dust and moisture-proof configuration, absolutely can not be saved.

    Irregular and variable load conditions

    Rubbish and ordinary materials are not the same, its density is not uniform, some places loose, some places lumps, and even mixed with stones, metal and other hard objects, it is difficult to control the load when grabbing.

    In addition, the impact load when the grab falls will also cause additional wear and tear on the structure and components of the crane. These uncertainties have to be taken into account in advance when selecting the type, to avoid equipment in a long-term unstable load state.

    Determine the required lifting capacity and grab volume

    Figure out the working conditions, the next step is to combine the daily handling capacity of the plant, determine the crane’s lifting capacity and grab volume – these two parameters directly determine the equipment can keep up with the pace of production, can not choose a small enough to use, can not choose a large waste of cost.

    Combined with the daily handling capacity (TPD) accounting needs

    First of all, we should clarify the daily processing capacity of the plant (unit: t per day, TPD), which is the core basis for calculating the lifting capacity and grab volume. For example, a waste incineration plant with a daily processing capacity of 800t and a small transfer station with a daily processing capacity of 200 t have completely different equipment requirements.

    We can simply calculate: assuming that the plant operates for 20 hours a day, the number of cycles that the crane needs to complete per hour (grasping, transferring, unloading) is about 15-20 times, combined with the average density of the rubbish, you can calculate the weight of the rubbish that needs to be grasped for each time, and then determine the rated lifting capacity of the crane.

    For example, 800TPD incineration plant, 40t of rubbish per hour, according to 16 cycles per hour, each time you need to grab about 2.5t, and then reserve a certain safety margin, choose 3-5 t of lifting capacity is more appropriate.

    If the daily handling capacity reaches more than 1,000t, the lifting capacity should be more than 10 t to meet the production demand.

    Grab Cranes

    Grab Cranes

    The key to the selection of grab is to adapt to the characteristics of the rubbish.

    Grab is the crane’s gripper, selection is not right, and then the good use of the crane can not play a role. The commonly used grabs on the market are mainly divided into two types, hydraulic and electro-hydraulic, and orange flap grabs and shell-shaped grabs, we have to choose according to the type of rubbish.

    Hydraulic grabs have large gripping force and tight closure, suitable for viscous, uneven density of domestic rubbish, and are not prone to leakage and jamming problems; electro-hydraulic grabs are relatively simple in structure, easier to maintain, and are suitable for loose rubbish, such as crushed industrial rubbish.

    From the shape point of view, the orange petal grab is suitable for blocky and granular rubbish, with large grabbing volume and high efficiency, such as the crushed rubbish in waste incineration plants; the shell-shaped grab has a small closing gap and is suitable for loose and finely crushed domestic rubbish, which can effectively prevent leakage of materials and reduce the workload of on-site cleaning.

    In addition, the volume of the grab should be matched with the lifting capacity and the density of the rubbish – for dense rubbish, choose a small volume grab; for loose rubbish with low density, choose a large volume grab, so as to ensure that the weight of each grab is up to the standard and to enhance the operational efficiency.

    Sufficient safety margin must be reserved

    The load of the waste treatment plant is unstable, so the lifting capacity must be reserved for safety margin, not just stuck to the actual demand to choose.

    Generally speaking, the dynamic load factor should be considered – when the crane is gripping, lifting and running, the load will produce a certain impact force, and this impact force is the dynamic load. It is generally recommended to reserve a safety margin of 10%-20%, for example, if you actually need to grab 3t of rubbish, choose a lifting capacity of 3.5-4t to avoid overloading operations.

    At the same time, the equipment must be equipped with a reliable overload protection system, which can automatically stop the crane once the load exceeds the rated value, preventing equipment damage, falling rubbish and other safety accidents, which is also the basic requirement for safe operation of rubbish plants.

    Choose the right crane structure

    The structure of the crane directly determines its stability, lifting height and operating range. Combined with the size of the rubbish pit of the rubbish plant and the operational requirements, the selection of single girder and double girder, as well as the matching of span and coverage, are the key considerations.

    Bridge cranes for waste treatment plants

    Bridge cranes for waste treatment plants

    Priority to double girder structure for rubbish plant

    Many purchasing friends will consider choosing single girder grab type overhead travelling crane in order to save the upfront cost, but combined with the working condition of rubbish plant, I recommend giving priority to double girder structure – not that single girder is bad, but double girder is more suitable for the heavy load and high frequency operation demand of rubbish plant.

    The main girder of double girder crane is more rigid and stable, and it is not easy to deform the main girder when grabbing heavy loads of rubbish and frequently starting and stopping.

    Moreover, the lifting height of double girder is higher, which can make full use of the vertical space of the rubbish pit and increase the rubbish storage capacity.

    In addition, double girder cranes have a larger operating range and can be paired with larger grabs to enhance operational efficiency.

    On the contrary, single girder cranes, rigidity and stability is relatively weak, long-term heavy-duty operation is prone to failure, and the lifting height and operating range is limited, suitable for small daily handling capacity, light load of small waste transfer stations, such as daily handling of 500t or less of the plant, if a large incineration plant, choose a single girder later will certainly be a problem.

    Span and coverage to match the size of the rubbish pit

    Crane span, to strictly match the width of the rubbish pit, the core requirement is ‘full coverage, no dead ends’ – that is to say, when the crane is running, the grab can cover the entire area of the rubbish pit, there will not be a corner of the rubbish can not catch the situation.

    For example, if the width of the pit is 20m, the span of the crane can be chosen to be about 22m, leaving 1-2m of safe running space to avoid collision with the edge of the pit and the columns of the plant when the crane is running. If the rubbish pit is longer, you can match multiple cranes, or choose a large span double girder crane to ensure that the entire rubbish pit can be covered.

    Grab Type Bridge Crane

    Grab Type Bridge Crane

    In addition, the need for precise positioning should also be considered – the position of the inlet of the waste incineration plant is fixed, and the crane is required to feed the waste into the inlet accurately, which requires the crane’s operation and positioning accuracy to be high enough to avoid feeding deviation, which will affect the incineration efficiency.

    Selection of operating level and core components

    Cranes in waste treatment plants need to withstand high-frequency, heavy-duty operations for a long time, so the operating level and the selection of core components must be durable and reliable.

    Operating level must meet the heavy-duty standard

    As we mentioned earlier, the cranes in the waste plant need to reach FEM A7/A8 class or CMAA E/F class, which corresponds to the requirements of heavy-duty and continuous operation, and can withstand frequent starts and stops and heavy-duty loads, and won’t wear out the components too quickly because of long-time operation.

    The choice of operating level directly determines the configuration of core components such as motors, gearboxes, brakes, etc. – heavy-duty level cranes will be paired with more durable motors and gearboxes, which can withstand high-frequency start-stop wear and tear; the braking performance of the brakes is also stronger, and can be used to stop the machine quickly and smoothly under heavy loads to ensure operational safety.

    Core components to adapt to high-frequency operation

    Motor, gearbox, brake, is the crane’s ‘three core components’, their quality directly determines the service life and operational stability of the equipment, selection must focus on.

    Motor, we should use heavy-duty motors suitable for high-frequency starting and stopping, the power should be matched with the lifting capacity and the frequency of operation, to avoid motor overloading and burning problems.

    Gearboxes should use wear-resistant, strong load-bearing capacity models, to adapt to frequent variable-speed operation, reduce gear wear

    Brake to choose redundant braking system, that is, double braking, even if one set of braking system failure, the other set can work normally, to avoid the safety hazards of stopping failure.

    In addition, cables and electrical interfaces should also be well protected, using wear-resistant, corrosion-resistant cables, electrical interfaces to do sealing to avoid dust, moisture intrusion, resulting in electrical short circuits.

    Selection of automation and intelligent control system

    Now more and more waste treatment plants, especially large-scale incineration power generation projects, will consider the automation function of the crane – automation not only reduces the workload of the operator, but also improves the operational precision and efficiency, and safeguards the incineration stability.

    Semi-automatic operation

    For small and medium-sized waste treatment plants with small daily handling capacity and relatively simple operating procedures, semi-automatic operation is sufficient.

    Semi-automatic operation is mainly controlled by remote control, the operator can be in the driver’s cab, or in the safe area around the rubbish pit, through the remote control to control the operation of the crane, the grabbing and unloading, without close contact with the rubbish, not only to improve the working environment of the operator, but also to enhance the safety of the operation.

    Grab Type Bridge Crane

    Grab Type Bridge Crane

    It should be noted that the semi-automatic operation of the crane, to ensure that the vision of the cab is good enough, the operator can clearly see the situation of the grapple and the rubbish pit, to avoid operational deviation; at the same time, it should be equipped with a simple positioning system, to facilitate the accurate delivery of the rubbish into the feeding port or the designated area.

    Fully automatic operation

    For large-scale waste incineration plants with a daily handling capacity of more than 1,000 tonnes, it is recommended to use a fully-automatic grab type overhead travelling crane, which can significantly improve operational efficiency and stability.

    The fully-automatic system mainly relies on PLC control and 3D rubbish pit scanning technology, which can scan the distribution of rubbish in the rubbish pit in real time and automatically plan the grabbing route to complete the grabbing, mixing, transferring and feeding of rubbish without manual intervention.

    Moreover, the fully-automatic system can achieve even mixing of waste, avoiding the accumulation of single waste, allowing fuller combustion in the incinerator, enhancing power generation efficiency and reducing environmental emissions.

    In addition, the fully-automatic crane can also be paired with a data monitoring system to provide real-time feedback on the operating status of the equipment, the amount of rubbish grabbed and the amount of material fed, which facilitates scheduling and management by the management personnel and realises the automated linkage of the entire production line.

    Anti-swaying and accurate positioning are essential features

    Regardless of whether it is a semi-automatic or fully-automatic crane, anti-swaying and precise positioning functions are indispensable – the operating space of the waste treatment plant is limited, and it is necessary to accurately feed the rubbish into the feeding port, once the grab swings, it will not only affect the operating efficiency, but also may collide with the plant equipment or the edge of the rubbish pit, which will lead to a safety accident.

    The anti-sway function is mainly controlled by a frequency converter (VFD), which can regulate the running speed of the crane, reduce the swaying amplitude of the grab, and allow the grab to run smoothly.

    Precise positioning function can be achieved through the encoder and positioning sensors to achieve precise start and stop of the crane and precise placement of the grab, ensuring that the rubbish can be accurately fed into the feed opening to avoid deviation.

    Corrosion protection and durability

    The high corrosion, dust and humidity environment of waste treatment plants is the main reason for the wear and tear of grab cranes, so anti-corrosion protection and durability configuration must be done sufficiently – this part of the investment can significantly extend the service life of the equipment, reduce the maintenance costs in the later stage, seemingly increasing the budget in the early stage, but in fact, it can save long-term operation and maintenance expenses. .

    Anti-corrosion paint to reach C4/C5 standards

    The main beams, end beams, trolleys and other main structures of the grab cranes in the waste treatment plant must be professionally anticorrosive, and the anticorrosive paint should be up to the C4/C5 standard – this standard corresponds to a highly corrosive environment, which can effectively resist the erosion of corrosive gases, such as hydrogen sulphide, ammonia, etc., and prevent the main structure from rusting and corroding.Specifically, the main structure should first do a thorough descaling treatment to remove the oxide skin and rust on the surface, and then apply primer and topcoat, the primer mainly plays the role of rust prevention, while the topcoat plays the role of corrosion and wear-resistant, and the thickness of the coating should reach the prescribed standard to ensure the anti-corrosion effect. In addition, the welded parts of the main structure, to do additional anti-corrosion treatment to avoid corrosion of the welded seams.

    Selection of closed trolley and stainless steel parts

    Crane trolley is the core running parts, easy to dust and corrosive gas erosion, so it is recommended to use closed trolley design – closed trolley can be motor, gearbox, electrical system and other core components sealed inside, to avoid dust and corrosive gas intrusion, reduce component wear and failure probability.

    At the same time, the trolley guide rail, wheels, hooks and other wear parts, it is recommended to use stainless steel or special treatment of wear-resistant and corrosion-resistant materials, these materials can resist corrosion and wear and prolong the service life of the components, reduce the frequency of replacement. In addition, the bucket body and chain of the grapple should be made of wear-resistant and corrosion-resistant manganese steel to cope with the wear and corrosion of the rubbish.

    Cable and electrical system protection

    Cable and electrical system is the nerve of the crane, once corroded or blocked, it will lead to equipment shutdown, so the protection must be in place.

    Cables should be selected wear-resistant, corrosion-resistant, waterproof special cable, the outer layer of the cable should be done to protect the casing, to avoid wear and tear or corrosion of the cable; electrical cabinets should be made fully sealed, the electrical interface should be selected waterproof and dustproof joints, to avoid the intrusion of dust and water vapour, resulting in an electrical short-circuit; at the same time, the electrical system should be made corrosion-resistant treatment, the selection of corrosion-resistant electrical components, to ensure that the electrical system operates stably.

    In addition, the cable wiring should be reasonable, to avoid the cable being squeezed or worn by the crane operation, but also to do a good job of fixing the cable to prevent the cable from loosening and falling off, triggering safety accidents.

    Essential safety features of waste treatment plant

    The operating conditions of waste treatment plants are complex and the safety risk is high, so the safety features of cranes, should never be omitted – every safety configuration is an important barrier to ensure the safety of personnel and equipment, and is also the basis for meeting the compliance requirements of the regulatory authorities.

    Redundant braking system

    As we mentioned earlier, cranes in waste plants need to start and stop frequently, and the load is unstable, so they must be equipped with a redundant braking system, that is, double braking – a set of main braking system, a set of backup braking system, even if the main braking system fails, the backup braking system can also work normally, to avoid cranes from stopping and failing to work, load falling and other safety accidents.

    At the same time, the braking performance of the brake to meet the requirements of heavy-duty operations, can be fast and smooth stopping under heavy loads, the braking distance should be controlled within the specified range to ensure operational safety.

    Basic safety devices should not be missing

    In addition to redundant braking system, there are several basic safety devices are necessary: overload protection system, real-time detection of the load weight, once more than the rated value, automatic shutdown and alarm to prevent overloading operations;

    Lifting height limiter, can limit the maximum lifting height of the grab, to avoid the grab lifting too high to crash the main beam; running stroke limiter, can limit the running range of the crane, to avoid the crane overrun to crash the plant columns;

    Emergency stop button, distributed in the driver’s cab, the ground operating station and the key parts of the equipment, in case of an emergency, can immediately cut off the power shutdown, to avoid the expansion of the accident.

    Fire cables and monitoring and alarm systems

    For waste incineration plant, but also equipped with fireproof cable – incinerator around the high temperature, and there are fire hazards, fireproof cable can be maintained in the high temperature environment, even if a fire, but also can slow down the burning speed of the cable, for the evacuation of personnel and equipment downtime to buy time.

    At the same time, the crane should be paired with a monitoring and alarm system, real-time monitoring of the operating status of the equipment, including motor temperature, gearbox oil temperature, braking system status, load weight, etc., once the anomaly occurs, an alarm signal can be immediately issued to remind the management staff to deal with timely!

    Special Requirements for Electrical System

    Waste treatment plant electrical system, especially incineration plant, need to deal with high temperature, high corrosion, frequent start and stop conditions, so the electrical system selection, to meet the special requirements to ensure stable operation.

    Heat resistance to adapt to the incineration plant’s high-temperature environment

    Incineration plant feeding area and incinerator surrounding, high temperature, so the components of the electrical system, to choose heat-resistant type, can maintain normal operation in a high temperature environment, to avoid the problem of component aging, burning. For example, motors, frequency converters, electrical cabinets, etc., should be selected high temperature models, electrical cabinets should also be done to dissipate heat treatment, to avoid the internal temperature is too high, affecting the operation of electrical components.

    Backup power supply and remote diagnostic function

    Most of the waste treatment plants are in continuous operation, once the power failure, crane shutdown will lead to rubbish accumulation, affecting the production, so the electrical system should be equipped with standby power supply – standby power supply can be used to provide temporary power for the crane in case of a power failure to ensure that the crane can complete the remaining rubbish transfer and shutdown operations, avoiding rubbish accumulation and equipment Damage.In addition, the electrical system should be equipped with remote diagnostic function, so that the management personnel can check the operating status of the electrical system of the equipment in real time through the remote terminal, find out the hidden dangers of the electrical faults in time, and arrange for the maintenance in advance to avoid the expansion of the faults; at the same time, the remote diagnostic function can also realise the remote troubleshooting and the maintenance guidance to reduce the on-site workload of the maintenance personnel and improve the maintenance efficiency.

    Docking to plant DCS system

    Large waste treatment plants, especially incineration power generation projects, will have their own DCS (Distributed Control System), so the crane’s electrical system, to be able to dock the plant’s DCS system, to achieve data interoperability and linkage control.

    By docking the DCS system, the crane’s operating data, the amount of rubbish grabbed and the amount of feed can be uploaded in real time to the central control room of the plant, where the management staff can unify the scheduling and management, and realise the linkage of the crane and other production line equipment such as incinerator and sorting equipment, so as to improve the operating efficiency of the whole plant.

    At the same time, the DCS system can also monitor the operating status of the crane in real time, and once abnormalities occur, it can immediately send out an alarm signal, which is convenient for timely treatment.

    Maintenance and after-sales support

    Waste treatment plant crane is the core equipment, once the failure, it will affect the operation of the entire production line, so the maintenance and after-sales support, but also the selection of the type must focus on the factors to consider – choose a reliable after-sales manufacturers, can reduce the later operation and maintenance trouble, to ensure that the equipment for long-term stable operation.

    Predictive maintenance system

    It is recommended to use cranes equipped with predictive maintenance system – predictive maintenance system can monitor the operating status of the equipment through sensors in real time, including motor temperature, gearbox oil temperature, bearing wear, cable insulation, etc., to detect potential equipment failures in a timely manner, and send out early warning signals to remind the management personnel to arrange for maintenance in advance. This way of maintenance can avoid sudden breakdowns.

    This kind of maintenance can avoid downtime caused by sudden failure and reduce production loss, and also prolong the service life of parts, reduce maintenance cost and realise the fine management of equipment.

    Spare parts supply and after-sales response time

    When selecting the model, we should ask the manufacturer’s spare parts supply and after-sales response time, to avoid the shortage of spare parts resulting in prolonged down time. At the same time, the manufacturer’s after-sales response time should be controlled within 24 hours, it is best to have a local service network, once the equipment failure, the manufacturer can quickly go to the door to deal with the problem, solve the problem in time and restore the equipment to run.

    In addition, it is also necessary to ask about the qualifications of the manufacturer’s after-sales team to ensure that the after-sales personnel have professional maintenance technology and can quickly troubleshoot and solve the problem .FAT and SAT tests must be in place Before the equipment leaves the factory and after installation and commissioning,
    FAT (Factory Acceptance Test) and SAT (Site Acceptance Test) must be in place – these two tests are the key to ensuring the quality and performance of the equipment, and can avoid unqualified equipment from being put into use.
    FAT test is mainly carried out in the factory of the manufacturer, focusing on testing the performance of the equipment, safety configuration, operational stability, etc., to ensure that the equipment meets the design requirements and relevant standards; SAT test is carried out at the site of the waste treatment plant, focusing on testing the equipment’s installation accuracy, operational status, docking compatibility, etc., to ensure that the equipment can be adapted to the plant’s working conditions and normal operation.
    Procurement personnel to participate in the two tests, the test results to confirm, once the problem is found, and timely request the manufacturer to rectify, to ensure that the equipment meets the requirements, and then acceptance.

    Remote-Controlled Grab Crane for Dust Environments

    Remote-Controlled Grab Crane for Dust Environments

    Selection of common misconceptions

    Many purchasing friends in the selection, easy to be biased by some of the wrong ideas, resulting in improper selection, and a variety of problems later. These common misunderstandings, must be avoided in advance.

    The first misunderstanding, in order to save upfront costs, choose a light load level crane. It is not worth the loss.

    The second misunderstanding, ignore the anti-corrosion protection configuration. The corrosive environment of the rubbish plant, the crane’s loss is great, if the anti-corrosion protection is not in place, the equipment can not be used for 1-2 years on the main structure of the corrosion, damage to the components of the problem!

    The third misunderstanding, underestimation of the frequency of operation cycle, resulting in the equipment can not keep up with the rhythm of production. Many purchasing in the calculation of the lifting capacity and grab volume, only considered the daily handling capacity, but underestimated the hourly frequency of the operating cycle, affecting the operation of the production line.

    The fourth misunderstanding, do not consider the automation upgrade needs, only choose the basic model equipment.

    Nowadays, the automation level of the waste disposal industry is getting higher and higher, and many plants will be upgraded to automation in the later stage. If the crane selected in the early stage does not support automation upgrading, it will need to invest extra money in transformation in the later stage, and even need to replace the equipment, which will increase the unnecessary expenses.

    The fifth misunderstanding, ignore the after-sales support, only look at the price of the equipment.

    Many purchasing feel that the quality of the equipment is the most important, after-sales is not important, but once the equipment of the rubbish plant fails, it will affect the production, if the after-sales response is not timely, the supply of spare parts is not in place, the downtime will be greatly extended, resulting in huge production losses – choose a reliable after-sales manufacturers, more important than choosing a low-priced equipment.

    Case reference

    In order to let you understand the selection process more intuitively, we share with you a selection case of 800TPD domestic waste incineration plant for your reference.

    The core requirements of this plant: 800 tonnes of domestic waste treatment per day, 24-hour continuous operation, the size of the rubbish pit is 40 m long, 20 m wide and 8 m deep, the rubbish needs to be accurately fed into the feed port of the two incinerators, and the equipment is required to have semi-automatic operation, anti-swinging and accurate positioning, and anti-corrosion protection should be adapted to the highly corrosive environment.

    The final selection plan: choose two sets of 10t double girder grab type overhead travelling crane, with a span of 22m, a lifting height of 16m, and an operating level of FEM A8, to meet the requirements of heavy-duty and high-frequency operations;

    The grapple is a hydraulic shell-shaped grapple with a volume of 5 cubic m, which is suitable for the characteristics of domestic rubbish and avoids leakage and jamming; it is equipped with a semi-automatic remote control system, which allows the operator to operate it in a safe area, and it is equipped with an anti-swinging and precise positioning function, which ensures that the rubbish is accurately fed into the feeding opening.

    Purchasing Selection Checklist

    In order to facilitate quick checking when selecting models, a procurement selection checklist has been compiled, against which you can check one by one to avoid missing key points:

    1. Daily handling capacity (TPD): clarify the daily handling capacity of the plant, and account for the crane’s lifting capacity and grab volume;
    2. Waste pit dimensions: confirm the length, width and depth of the waste pit, matching the span and lifting height of the crane;
    3. Operating level: ensure that the equipment reaches FEM A7/A8 class or CMAA E/F class to meet the requirements of heavy-duty and high-frequency operations;
    4. Crane structure: according to the working conditions, give priority to the double girder structure to ensure the span can cover the rubbish pit without dead angle;
    5. Grab selection: according to the type of rubbish, select hydraulic/electro-hydraulic grab, orange flap/bay grab to match the density of rubbish;
    6. Automation level: according to the scale of the plant, choose semi-automatic or fully automatic operation, equipped with anti-swing and precise positioning function;
    7. Anti-corrosion protection: confirm that the anti-corrosion paint reaches C4/C5 level, choose closed trolley and stainless steel parts, and provide good cable and electrical protection;
    8. Safety Configuration: Ensure that it is equipped with safety devices such as redundant braking, overload protection, emergency stop, etc., and meets the safety compliance requirements;
    9. Electrical system: select heat-resistant and corrosion-resistant electrical components, equipped with backup power supply and remote diagnostic function, which can be docked to the DCS system of the plant;
    10. After-sales support: confirm that the manufacturer has mature waste treatment plant cases, can provide 24-hour after-sales response, local service outlets, and timely supply of spare parts;
    11. Acceptance test: Confirm that the manufacturer can provide FAT and SAT tests to ensure that the quality and performance of the equipment meet the requirements;
    12. Relevant certificates: to confirm that the equipment has the production licence of lifting machinery, ISO9001 quality certification and other relevant qualifications, in line with industry standards.

    High Frequency FAQ

    Why do waste treatment plants give priority to double girder grab type overhead travelling crane?

    A: Mainly because the rubbish plant needs heavy load, high frequency, continuous operation, the main girder of double girder crane is more rigid, better stability, can withstand heavy loads and frequent starting and stopping, not easy to deformation.

    How long is the service life of grab type overhead travelling crane for rubbish treatment plant in general?

    A: Under normal circumstances, good anti-corrosion protection and routine maintenance, the service life of the equipment can reach 15-20 years. The specific service life mainly depends on the anticorrosion protection configuration, the quality of core components and routine maintenance – if the anticorrosion protection is in place, the core components are of high quality, and regular maintenance, the service life can be longer; on the contrary, if the anticorrosion protection is not in place, or the maintenance is not timely, the service life may be only 5-10 years.

    Can grab cranes in waste treatment plants be operated fully automatically?

     Yes. Nowadays, most of the large-scale waste incineration plants use fully-automatic grab type overhead cranes, which can realise automatic grabbing, transferring, mixing and feeding of waste through PLC control and 3D waste pit scanning technology, without manual intervention. Moreover, the fully automated system can enhance operational efficiency and feeding uniformity, improve incineration effect, and can be paired with a data monitoring system to realise the fine management of the equipment, which is suitable for the automation development trend of the waste treatment industry.

     How to calculate the size (volume) of the grab?

    A: The volume of the grab is mainly calculated according to the daily processing capacity, the number of operating cycles and the density of rubbish, the core formula is: Grab volume (cubic m) = Hourly processing capacity (t) ÷ Number of cycles per hour ÷ Density of rubbish (t/cubic m). For example, 800t of rubbish per day, 40t per hour, 16 cycles per hour, rubbish density of 0.8 t / cubic m, then the grab volume is 40 ÷ 16 ÷ 0.8 ≈ 3.125 cubic m, the actual selection of the type of grab can be selected 3-4 cubic m, to reserve a certain amount of margin.

    Waste incineration power generation project grab crane, what are the relevant certifications required?

    A: There are three main types of core certificates: one is the production licen for lifting machinery, the second is the ISO9001 quality system certification, and the third is the safety certification, including the certification of overload protection, braking system and other safety devices, to ensure that the equipment is in line with the ‘Safety Regulations for Lifting Machinery’.

    Conclusion

    Grab type overhead travelling crane is the core equipment of waste treatment plant, for waste treatment plant, the core of selection is not to choose the cheapest, not to choose the most advanced, but to choose the most suitable – suitable for the plant’s daily capacity, waste characteristics, operating conditions, taking into account the heavy-duty, anticorrosion, safety and automation requirements, in order to achieve the stable long-term operation of equipment, and enhance the whole plant. Long-term stable operation, enhance the operational efficiency of the entire plant, and obtain a higher long-term ROI.

    Henan Mine Crane, as a deep-rooted lifting machinery field of strength manufacturers, in the design and production of waste treatment plant grab type overhead travelling crane, just fit this ‘fit first’ selection concept, it is worth focusing on.

    Waste disposal industry working conditions are special, the needs of different plants vary greatly, there is no uniform selection standard, if you are not sure how to select their own plant conditions, or do not know how to match the parameters of the equipment, you may wish to contact us, we are relying on its many years of production and manufacturing of grab cranes.

    We rely on its many years of manufacturing experience and perfect technical system, combined with our industry selection experience, according to your plant’s daily handling capacity, rubbish pit size, operational needs, free of charge to issue an exclusive selection program me, to help you avoid the selection of misunderstandings, to select the appropriate, durable, cost-effective Henan Mine Crane equipment.

    Submit your rubbish pit layout and daily handling capacity requirements, to provide you with detailed technical proposals, including crane equipment configuration, parameter details, anti-corrosion solutions and after-sales protection, to help your rubbish treatment plant to achieve efficient, stable and safe operation.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Choose a Straddle Carrier for Container Yard? Complete Buying Guide

    How to Choose a Straddle Carrier for Container Yard? Complete Buying Guide

    How to Choose a Straddle Carrier for Container Yard? Complete Buying Guide

    With global container freight volumes still rising, both coastal hub ports and inland container depots (ICDs) are on the lookout for container handling solutions that can boost efficiency and cut labour costs. Straddle carriers are the best choice for handling equipment in many depots, because they can adapt to different yard layouts.
    You’ll get the hang of the equipment in no time.


    Basic Understanding of the Equipment

    The main parts of the machine include the gantry structure, lifting frame, telescopic container lifting device, steering system, power unit, hydraulic system, operator cab, and safety sensors. It’s pretty straightforward: you put a container to be retrieved, lift it to a safe height, move it around the yard, and then put it down to stack it – and all of this is done by one unit on its own.

    Here are a few things to think about when choosing:

    Equipment Type Initial Investment Throughput Labor Demand Yard Flexibility Stacking Height Best For
    Straddle Carrier Medium High Low Very high 2-4 layers Medium-large flexible yards
    RTG Crane Medium-high Medium-high Medium Low 4-6 layers Fixed container blocks
    Reach Stacker Low-medium Medium Medium High 1-3 layers Small yards & transfer
    Terminal Tractor + Chassis Low Medium High High 0 layer Horizontal transport only

    When picking a container yard straddle carrier, the first thing to do is to work out the actual workload. First, you need to work out the average daily container throughput, peak-hour throughput, and truck turnaround time. Then, you need to work out the ratio of inbound to outbound containers, the proportion of empty versus full containers, and whether there are any special container types, like refrigerated or hazardous materials containers.

    Container Straddle Carrier by Henan Mine Crane

    Things to think about when choosing:

    Check how much work the yard can do and what it needs to be able to do that

    When picking a container yard straddle carrier, the first thing to do is to work out the actual workload. First, you need to work out the average daily container throughput, peak-hour throughput, and truck turnaround time. Then, you need to work out the ratio of inbound to outbound containers, the proportion of empty versus full containers, and whether there are any special container types, like refrigerated or hazardous materials containers.

    Find out how much weight your load can hold and what kind of container you need to use it in.

    Stacker Truck Specifications: The rated payload is a key factor. For regular 20-foot and 40-foot standard containers, models with a 35–40 metric ton capacity are enough. But if you need 45-foot containers, double-container lifting or heavy-duty specialty containers, go for models with a 45–60 metric ton capacity.

    Making sure the stacking height and yard utilisation match up.

    The height you can stack them at directly affects how much space you have in the yard. The most common set-ups are 1-over-2 (2-tier stacking), 1-over-3 (3-tier stacking) and 1-over-4 (4-tier stacking).

    The higher the stacking level, the more storage space you get per unit area. But this means you need equipment with a higher lifting height, which costs more to buy, takes longer to operate and means the operators need better visibility. High-level stacking is great for yards on the outskirts of cities where land costs are high, and in core port areas. But for inland yards with plenty of land and fast turnover, 2–3-layer stacking is a better option.

    When picking the stacking height for straddle carriers, it’s worth thinking about space reserves for business growth over the next few years. There’s no need to go for the highest spec model straight away.

    Choosing the Right Power Type: Diesel, hybrid, electric

    Choosing the power type is a key part of the procurement decision. At the moment, the main options are diesel, hybrid, and fully electric. Lots of customers find it tricky to choose between diesel and electric straddle carriers.

    Diesel models have the most mature technology, are cheaper to buy at first, and don’t need as much extra infrastructure. They’re great for places with limited power supply or irregular operations, like inland stockpiles in the mining industry.

    Hybrid models add an energy recovery system to the diesel base, which reduces fuel consumption and emissions. They’re perfect for yards that want to cut energy consumption but don’t have charging infrastructure yet, making them a smart choice during a transitional phase.

    Diesel vs. Hybrid vs. Electric Straddle Carrier

    Item Diesel Straddle Carrier Hybrid Straddle Carrier Full Electric Straddle Carrier
    Purchase Cost Lower Medium Higher
    Operating Cost Higher (fuel) Medium Lower (electricity)
    CO₂ Emissions High Medium Zero on-site
    Maintenance More components Medium Fewer moving parts
    Infrastructure Requirement Low Low Charging station needed
    Best For Remote / high-duty yards Transition scenarios Green ports & urban yards

    We can adapt the steering systems to fit the yard layout.

    The steering system has a big impact on how adaptable the equipment is to the yard layout. There are a few different types, like two-wheel steering, four-wheel steering, and crab-style steering. When picking a straddle carrier steering system, it’s really important to make sure it’s the right width for the aisle in your yard and that it can handle the density of containers.

    For standard, open yards, two-wheel steering is enough, but for yards with narrow aisles and dense container areas, go for all-wheel steering straddle carriers, which have a smaller turning radius and are easier to manoeuvre.

    When you need to move stuff around quickly and carefully, like when you’re stacking things or working in narrow spaces, diagonal-steering straddle carriers are a better option. They mean you don’t have to keep adjusting the vehicle’s position, which saves a lot of time.

    Choose the automation levels you need.

    Lots of yards are currently upgrading digitally, and there are custom automated straddle carrier solutions available at different levels, so there’s no need to implement everything at once.

    The basic model that you drive yourself is great for small yards that need to be flexible.

    Semi-automated models have automatic positioning and collision-avoidance assistance, which makes them easier to use and more stable.

    With remote-control models, operators can control the vehicle from a central control room, keeping them away from harsh outdoor environments and reducing the number of on-site personnel.

    Fully automated, driverless models are kitted out with GPS, LiDAR, and obstacle detection to automatically plan routes and get jobs done. They work with the Terminal Operating System (TOS) and are great for automated container terminals, cutting labour costs.

    We can’t compromise on safety features.

    Whatever model you choose, you’ll need to make sure all the basic safety features are included. Stacker crane collision avoidance systems, load monitoring, wind speed alarms, emergency braking, automatic locking for lifting gear and panoramic video surveillance are all essential.

    For yards on the coast or in open areas, we need wind speed alarms and automatic locking devices that kick in when wind speeds go past safe limits. For hazardous materials yards, we might also add automatic fire suppression systems. And for yards where lots of vehicles are operating at the same time, we need a vehicle-to-vehicle distance anti-collision interlock function. When picking STF safety configurations, upgrades should be made as needed based on the yard’s risk level.

    Getting used to the local climate and environment

    The way plants do in different regions depends on the environment there.

    High-temperature ports in the Middle East need heat-resistant cooling designs and dust-proof sealing configurations. Engines and hydraulic systems have to be adapted for high temperatures, and cabs need to be equipped with high-capacity air conditioning. We’ve already used our customised straddle carrier solutions for high-temperature ports on loads of overseas projects in the high-temperature sector.

    In rainy yards in Southeast Asia, electrical sealing and rust/corrosion protection need to be strengthened to stop rainwater from eroding electrical components.

    Vans used for moving stuff around in coastal salt fog need anti-corrosion coatings that are made for the sea, with important parts made of materials that don’t rust to stop salt fog from damaging the equipment and making it last longer.

    Inland yards with high wind and sand must improve air filtration and dust-proof sealing to reduce sand and dust wear on transmission components.

    Just do the maths to work out the total cost of owning it.

    A lot of procurement problems come from focusing too much on the purchase price and not enough on the long-term operating costs. When you’re doing a total cost of ownership (TCO) analysis for straddle carriers, make sure you include the purchase price, fuel/electricity costs, maintenance expenses, tire wear, labor costs, downtime losses, and residual value.

    For instance, electric models might cost more to buy, but they use less energy and cost less to maintain. In situations where they’re used a lot, the extra cost can be made back in a few years. Diesel models might cost less up front, but you’ll be spending more on fuel and maintenance in the long run.

    When working out the total cost of ownership of an inter-yard truck, you’ve got to base it on a 10–15-year service life. That’s the only way to make sure you’re getting a good picture of the cost differences between the different options. It’s also worth calculating the full return on investment (ROI) for the inter-yard truck, including the benefits of labour savings, efficiency gains and reduced downtime.

    Assessment of the supplier’s capabilities

    It’s more important to choose the right supplier than to compare specs. When evaluating suppliers of inter-yard trucks, you shouldn’t just base your decision on price.

    It’s important to look at how good they are at customising their engineering, and whether they can adapt their designs to your yard layout and operational needs. Next, have a look at their project case studies to see if they’ve got experience implementing solutions at yards of a similar type and size.

    You should also check out their manufacturing qualifications and quality certifications, like international ones like CE and ISO. It’s also really important to have experience with automation and remote diagnostics for container handlers. When it comes to overseas projects, it’s really important to focus on after-sales support, like having a global network of spare parts, setting up and getting started on containers, and staff training.

    As a professional straddle carrier manufacturer, Henan Mine Crane offers a full range of services, from designing solutions and manufacturing to installing, setting up, and maintaining your crane over its lifetime. We make customised container straddle carriers that are just right for yards in different regions around the world.

    Here are some common mistakes to watch out for when choosing your models.

    If you only compare the price you pay upfront, you might end up with a low-cost model that breaks down a lot and is off the road a lot, which can end up costing you more in the long run.

    If you go for high-stack models without thinking about the yard layout, you might find yourself with too narrow aisles and difficulty moving equipment around, which can really mess up your efficiency.

    If you don’t think about how things might change in the future and only go for diesel models now, you might have to pay a lot more to adapt later when the rules about the environment get stricter.

    If you don’t think about how your supplier can help you after you’ve bought something, you might not get the parts you need when you need them. For example, you could be waiting months for replacement parts, which could cost you more than the price difference between the equipment models.

    Not thinking the cost of replacing tyres will be as high as it is. If the ground conditions are poor, tyres wear out quickly, so when choosing models, check the tyre specifications and durability.

    Here are some recommended configurations for different scenarios.

    We’ve got these small inland container depots (ICDs). Go for 35–40 metric-ton diesel models with 2–3-layer stacking and basic manual operation – you’ll get the best bang for your buck and it’ll be a breeze to keep them in good nick.

    Medium-sized dry port logistics parks: Go for 40–45 metric-ton hybrid or electric models with 3-layer stacking and semi-automated assistance. These are great for balancing efficiency and environmental sustainability, and they’re perfect for medium-to-large-volume throughput.

    Large international container terminals: Go for 45–60-metric-ton models with 3–4-layer stacking. You can upgrade these to remote control or fully automated operation, integrate with the terminal’s TOS system, and they’re suited for high-throughput operations.

    High-Temperature Ports in the Middle East: Diesel or hybrid models with extra heat resistance, dustproofing and protection against corrosion, as well as stronger cooling systems, to handle extreme heat.

    Inland Logistics Hubs in Africa: Choose proven diesel models with simple, reliable designs and readily available, interchangeable parts, suitable for environments with limited maintenance resources.

    Frequently Asked Questions

    How many containers is a straddle carrier able to handle in an hour?

    With the standard settings, one machine can do between 15 and 25 lifts in an hour. The exact number depends on things like transport distance, stacking height, and how complex the container is. Shorter distances and lower stacking heights usually result in higher efficiency.

    What stacking height offers the best bang for your buck?

    For most medium-sized yards, a 1-over-3 stack (3 layers) is the best deal, giving you the best balance between storage space and how easy it is to use, so you get the best bang for your buck.

    Which is better value for money, a diesel or electric model?

    It depends on when it’s open and how much energy it costs where you are. In places where they operate for longer on average and electricity is cheaper, electric models have a shorter payback period. In places where the power is not on all the time or you can’t get to it easily, diesel models are a safer bet.

    How long do you think a container handler usually lasts for?

    With a bit of TLC, the main structure should last you 15–20 years, and the powertrain and wear-and-tear parts just need to be replaced every now and then. Pairing the equipment with a container handler predictive maintenance system can make it last even longer.

    And finally, here’s the conclusion.

    Choosing the right container handler is all about balancing how well it works in practice, how flexible it is, how much it costs to own, and whether it can be upgraded in the future. You shouldn’t just choose the model with the highest specifications.

    To choose a solution that matches your company’s development needs and consistently delivers value over the next ten to twenty years of operation, you need to look at yard throughput, stacking strategies, powertrain type, automation requirements, and supplier service capabilities.

    Get your own container handler solution just how you want it.

    If you’re picking a container handler for your yard, send us your annual throughput, yard layout diagram, stacking height requirements, average daily operating hours, powertrain preferences, and automation needs.

    The engineering team at Henan Mine Crane will recommend the best straddle carrier configuration for you, and they’ll also provide customised yard layout recommendations and a full life-cycle cost analysis.

    You can also download the free “Container Yard Equipment Selection Checklist” to help your procurement team organise technical requirements and compare proposals from different straddle carrier suppliers more efficiently.

    Henan Mine CraneDiscuss your requirements ↗