Engineering · Manufacturing · Project support
info@hnksglobal.comWhatsApp +86 18836207779 ↗

作者: YUWEI, YUWEI

  • How to Select Rail-mounted Gantry Cranes for Automated Port Operations

    How to Select Rail-mounted Gantry Cranes for Automated Port Operations

    How to Select Rail-mounted Gantry Cranes for Automated Port Operations

    This article provides port planners, terminal operators and equipment procurement engineers with a set of scientific and systematic rail-mounted gantry cranes (RMG) selection framework, which covers the essential differences between RMG and RTG, evaluation of key technical specifications, automation level and control system integration, energy solutions and whole life cycle cost control, safety compliance standards, as well as mainstream supplier evaluation and procurement testing of the whole process strategy.

    Why RMG is the Mainstream Choice for Automated Ports

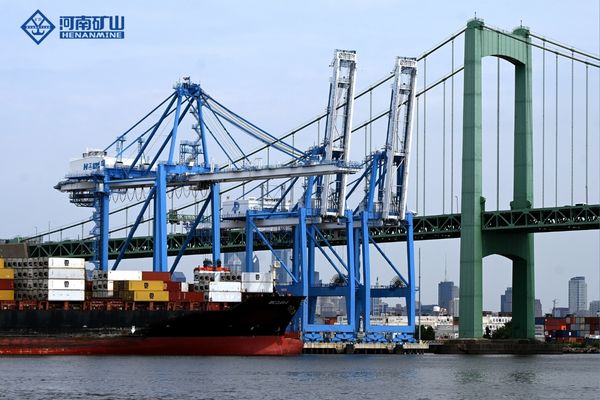
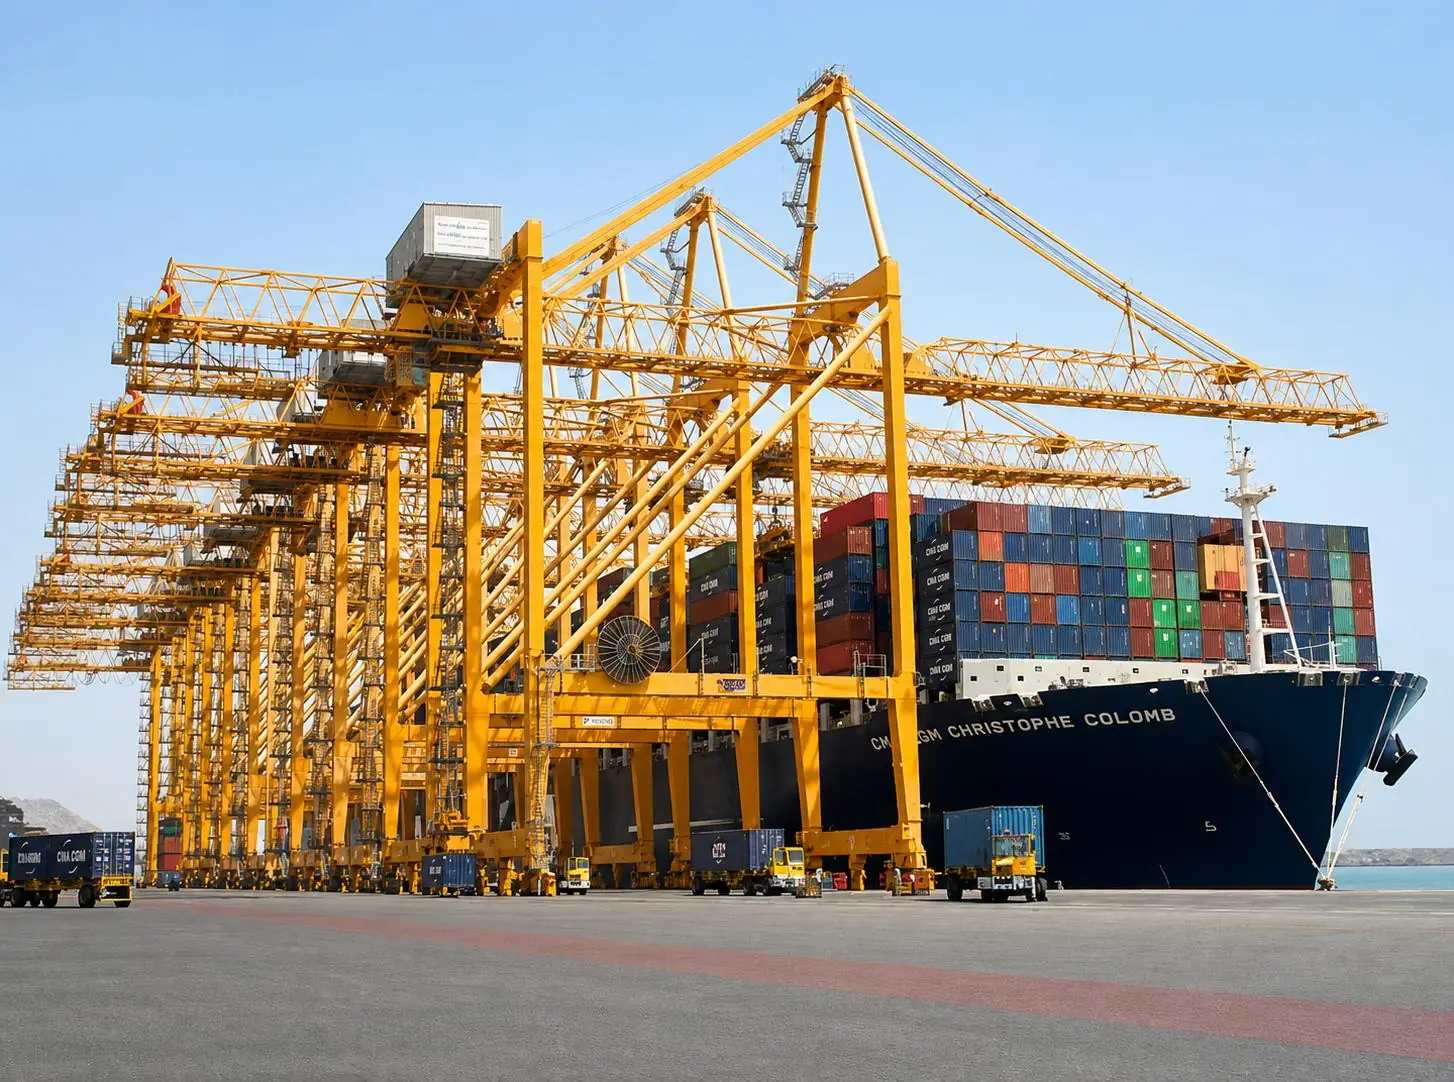
    Continued growth in global container throughput is reshaping the logical boundaries of port equipment decision-making. 2024 will see the Shanghai port handling more than 50 million standard containers (TEUs), with hub ports such as Singapore and Rotterdam expanding their throughput capacity at the same time, which means that any single wrong equipment selection could result in hundreds of millions of dollars in long-term losses.

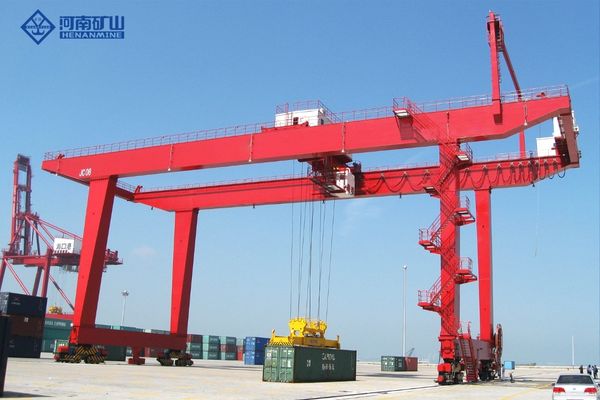
    In this context, Rail-Mounted Gantry Crane (RMG) is becoming the preferred yard equipment for large-scale automated terminals due to its high-precision feature of fixed rail operation.

    Difference in Automation Realisation Path between RMG and RTG

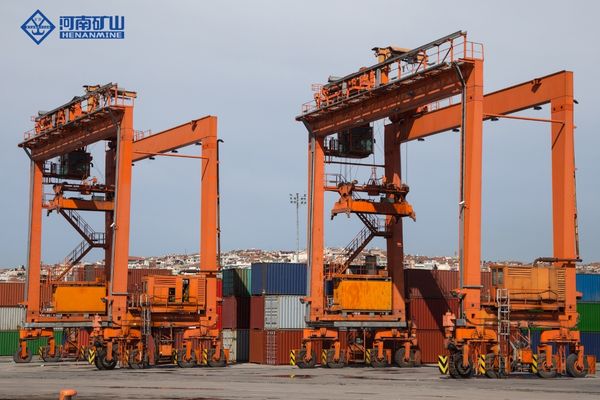
    The core difference between RMG and RTG lies in the automation path: RTG relies on rubber tyre movement, which is prone to positioning errors and difficult to achieve full automation;

    RMG runs along a fixed track with controllable trajectory and can integrate laser positioning and other technologies to achieve unmanned operation. According to the China Communications and Transportation Association data, the current domestic inland port RTG accounted for 95%, the industry predicts that, with the automation and environmental protection needs to improve, RMG will become the mainstream yard equipment in the future.

    RMG and RTG Economic Boundaries and Site Suitability

    From the point of view of economy and site suitability, for large ports with annual throughput of over 500,000 TEU, the higher initial investment of RMG can be covered by lower operating costs and higher site utilisation.

    Its fixed track can increase the density of stacked containers, which is effective when deployed in high-density terminals such as the Port of Singapore; while small and medium-sized ports and sites with variable layouts are more suitable for RTGs with flexibility advantages.

    Systematic Engineering Attributes of RMG Selection

    For large-scale automated ports, the selection of RMGs should not be seen as a simple equipment purchase, but rather as a systematic engineering decision covering civil, electrical, control, information, and operation modes.

    The next section of this paper provides a selection framework that can be directly applied to RFQs and internal decision making, based on five dimensions: technical specifications, level of automation, energy solutions, safety compliance and supplier evaluation.

    Core Technical Specification Evaluation

    Lifting Capacity

    RMG selection requires a clear definition of the core benchmark parameter of lifting capacity, which directly determines the complexity of the equipment structure, the manufacturing cost and the match with the yard’s operational needs.

    Currently, the rated lifting capacity of RMGs in mainstream ports is concentrated in 35 tonnes, 40.5 tonnes and 50 tonnes, and the heavy-duty model with double containers can reach up to 65 tonnes, such as the customised model provided by Liebherr for the Port of Montreal-Termont in Canada.

    Span and Lift Height

    Span (spacing between the outer edges of the two tracks) is the key to the density of the yard layout, the mainstream range of 25-80 metres, the larger the span of a single unit to cover the number of container columns more, suitable for the port of land constraints;

    The lifting height is expressed as ‘1 over N’, commonly 1 over 4 (small and medium-sized terminals), 1 over 5-6 (large ports), and the special model for empty containers can be up to 1 over 8, such as the model provided by ZPMC for the new port of Busan in South Korea, with a lifting height of 26.8 metres, which can increase the container capacity by more than 30%.

    Operation Efficiency and Spreader Selection

    The daily handling capacity of excellent RMG single machine should be more than 300 TEU, and the high-end fully automated model can stably operate more than 30 containers per hour. Spreader selection needs to match the box type:

    Standard 20/40 feet boxes can be used telescopic spreader, mixed 20/40/45 feet boxes need full telescopic rotatable spreader; at the same time, it is necessary to reasonably match the running speed of the big car and the small car, and the procurement specification should specify the rated speed, acceleration requirements and FAT measurement data.

    Requirements for Equipment Working Level

    The working level of the equipment (Duty Cycle) determines the durability of structural components and mechanism, and it should refer to FEM or equivalent ISO standard (A1-A8), and the high-frequency operation of port containers requires A7-A8 level, and there are clear requirements on the design margin of main beam, trolley frame and electrical components, and the specification specifies the working level to prevent suppliers from bidding for low standards.

    Automation Level and Control System Integration

    Classification of Automation Levels and Applicable Scenarios

    RMG automation level is divided into three clear levels, procurement needs to be clearly positioned in the project planning stage:

    • Manned: The driver operates the machine directly from the cab, which is suitable for sites with small workloads and frequent layout changes;
    • Semi-automated mode (Semi-Automated): the system automatically completes the precise positioning of the spreader and the stacking action, and the driver is only responsible for the travelling of the big vehicle and the abnormal intervention, which can reduce the operation fatigue and improve the consistency of the operation;
    • Fully automated mode (A-RMG): no one intervenes in the whole process from truck scheduling to spreader loading, and the central control system unifies the scheduling, which has been stably operated in many top automated terminals in Europe and Asia.

    Core Technology Support of Fully Automated A-RMG

    The realisation of fully automated A-RMG relies on the synergistic fusion of multiple sensors and positioning technologies: laser ranging sensors provide millimetre-level positional feedback (high-end systems have an accuracy of ±25mm);

    The OCR camera system automatically reads the box number and compares it with the yard management data; the AI vision system is responsible for obstacle detection, box top inspection and anti-lifting correction; and the RFID tags can realise the secondary confirmation of container identity.
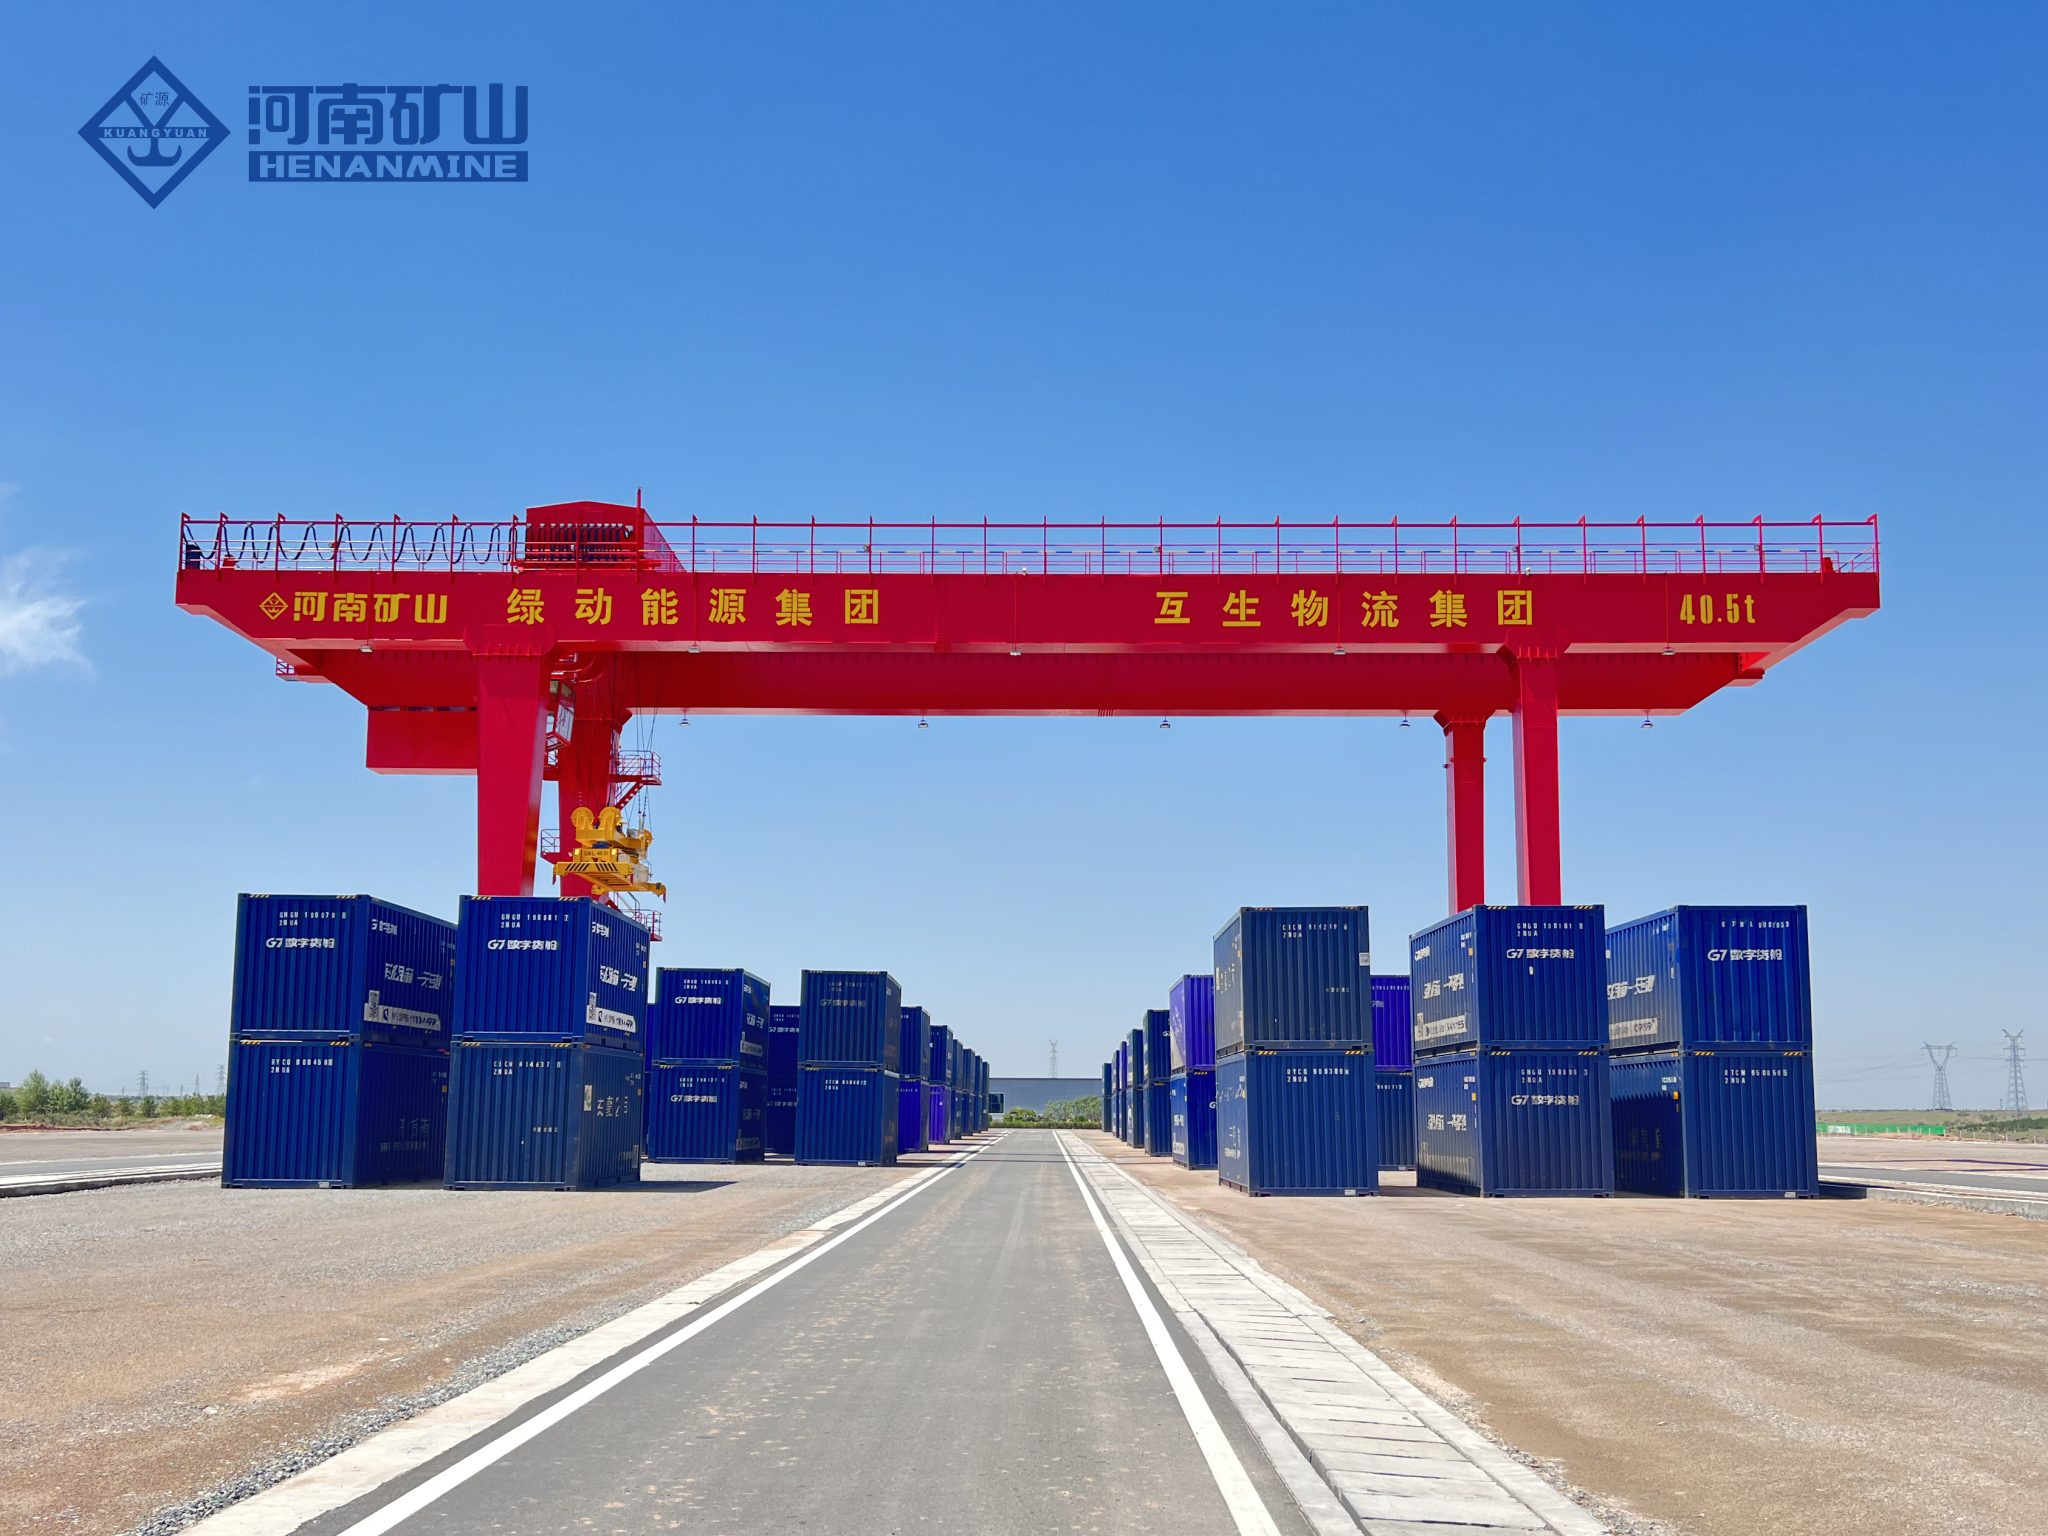
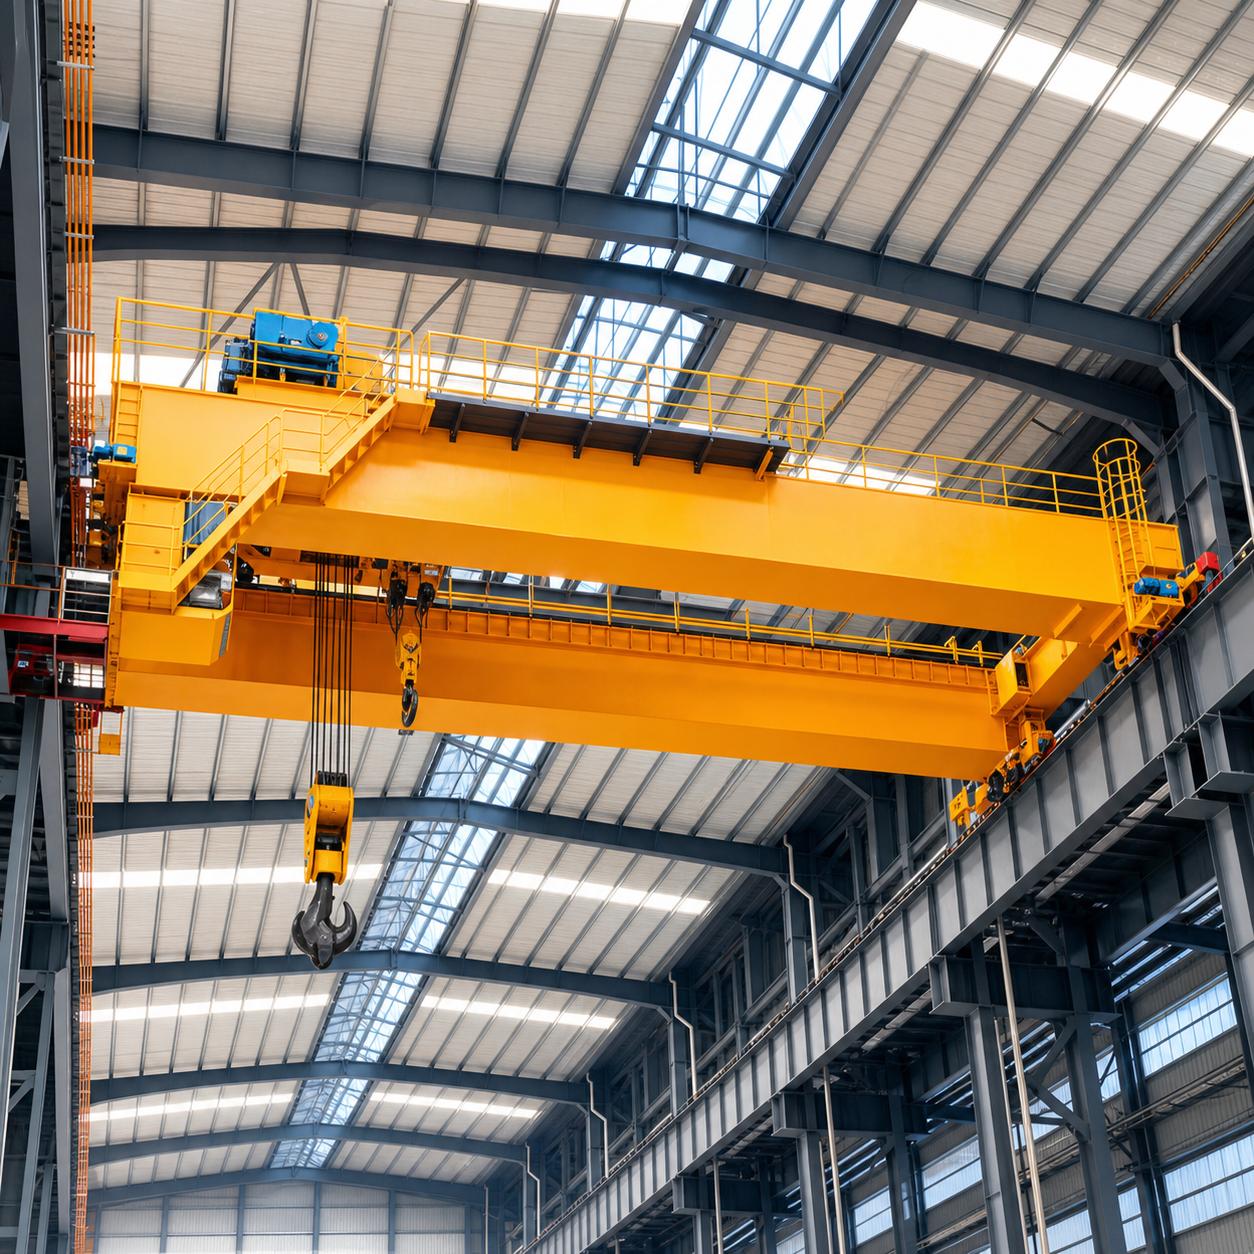
    RMG crane

    Integration Points of Automation RMG and TOS System

    The quality of integration between A-RMG and Terminal Operating System (TOS) is the core of determining the overall effectiveness of the system, and it is also a technical difficulty that is easily underestimated in procurement.

    A-RMG needs to exchange task commands and status data with TOS, maintenance management system, and berth scheduling module in real time, but most of the existing TOS lacks the native support of fine-grained status telemetry, which is easy to lead to the underestimation of integration works and risks.

    Purchasers need to focus on the compatibility analysis of existing TOS interfaces, and clarify the responsibility of TOS transformation in the contract; at the same time, control software upgrades, network security patches and other long-term cyclical costs, which need to be included in the total life cycle cost (TCO) model, and can not be regarded as a one-time investment.

    Automation Upgrade Path Suggestion

    For terminals that plan to gradually promote automation, it is recommended to choose a modular design solution with a smooth upgrade path of ‘manual → semi-automatic → fully automatic’.

    For example, the evolution path provided by Henan Mine Crane allows the terminal to go into operation in manual or semi-automatic mode at the initial stage, and then gradually switch to fully-automatic mode after the operation is stabilised, which effectively reduces the risk of one-off modification and the time of operation interruption, making it the preferred upgrade strategy for medium-sized ports.

    Energy System and Power Supply Solution

    Mainstream Power Supply Architecture and Applicable Scenarios

    The choice of power supply system is a strategic decision in RMG selection, directly affecting operating costs, site layout and carbon footprint. Currently, there are three mainstream power supply architectures, each with their own applicable scenarios:

    • Cable Reel: Suitable for longer travelling scenarios, flexible installation, but cable wear and tear requires regular maintenance;
    • Busbar: simple structure, high reliability, suitable for standardised sites with stable fixed track lengths;
    • Drag chain (Energy Chain): easy to install in short and medium travelling scenarios, with low maintenance costs.
    • Core Advantage: Regardless of the architecture, the RMG all-electric drive can significantly reduce fuel consumption and carbon emissions compared to diesel RTGs, which meets the requirements of green port policy compliance.

    Core Energy Saving Technology and Application Effectiveness

    The core of RMG energy saving lies in the combination of Variable Frequency Drive (VFD) and regenerative braking technology:

    • Regenerative braking system: The kinetic energy generated by the braking and lowering of the lifting mechanism can be converted into electrical energy and fed back to the power grid, reducing the energy consumption of the whole machine by 30%-40%, and saving considerable annual electricity costs for high throughput terminals;
    • Active Front End (AFE) rectifier units: Available from some leading manufacturers, this configuration reduces harmonic pollution while improving grid return efficiency, contributing to carbon accounting and reducing power infrastructure capacity requirements.

    Key points for Whole Life Cost (TCO) Modelling

    Rational selection needs to be based on modelling from a TCO perspective, clarifying the difference between initial CAPEX and long-term operating costs:

    • Initial Capital Expenditure (CAPEX): $1-6 million for a single machine (higher prices for fully automated, customised configurations), $500,000-1 million per hundred metres of track construction and laying, and automation and control system integration costs need to be estimated separately;
    • Advantage of operation cost: the labour, fuel and maintenance cost of RMG operation stage is much lower than diesel RTG;
    • Applicable scenarios: the TCO advantage of RMG is especially prominent in ports with an annual throughput of over 500,000 TEU and a life cycle of 15-20 years, especially adapted to markets with high labour costs and high fuel tax rates.

    Cutting-edge Technology Applications and Selection Requirements

    5G and digital twin technologies have become competitive standards for RMG energy management and O&M, and selection needs to be focused:

    • 5G wireless communication: with low-latency core features, it can realise real-time collaborative scheduling between RMG, AGV and TOS systems, efficiently reach closed-loop optimisation of yard operations and improve overall operational efficiency;
    • Digital twin platform: it can accurately simulate the operating status of cranes, test scheduling strategies and carry out training for operation and maintenance personnel, which can effectively shorten the commissioning cycle of the project and reduce the cost of commissioning and time cost;

    Selection requirements: the above technologies should be clearly written into the technical specifications as the core consideration dimension for supplier evaluation.

    Safety Standards and Compliance Requirements

    The safety design of port RMG should comply with the three core international standards of FEM, ISO 1161 and IEC 61508, which should be clearly cited in the contract and acceptance documents, and the automated RMG should be validated according to the SIL level design stipulated in IEC 61508.

    Anti-sway control system is the key to safe and accurate operation, excellent programme can control the spreader swing angle within ± 0.5 °, Konecranes ALC technology and domestic mainstream dynamic algorithms have reached the standard, the procurement needs to require the supplier to provide measured data and FAT validation procedures.

    Anti-collision system is the core of automated RMG safety, modern models integrated multiple detection mechanisms (ZPMC Busan Newport programme for high-end configuration), low-priced single-sensor programme is risky, procurement needs to be provided by the supplier of reliability data and operating records.

    Fail-safe braking system is an emergency safety guarantee, need to meet the power failure automatic clamping brake; coastal scenarios need to match the IP54 or more electronic control cabinets, IP65 or more exposed sensors, the relevant terms need to be included in the procurement of technical annexes.

    Procurement Strategy and Acceptance Test

    Cost structure classification and management points

    RMG project cost should be divided into three independent accounting buckets, and the procurement team should manage them separately and quantify them accurately:

    1. Mechanical and civil construction costs: including track, foundation, gantry main structure and other related expenditures;
    2. Mechanical & Electrical Upgrade Costs: covering upgrade and procurement costs for drive systems, encoders, spreaders, lock actuators, etc;
    3. Control and integration costs: covering PLC/RTU, safety controllers, edge computing devices and TOS system interface integration costs.
    4. Core management value: Separate quantification can accurately identify the source of cost overruns, and avoid the unreasonable operation of suppliers ‘suppressing equipment quotes and raising integration costs’.
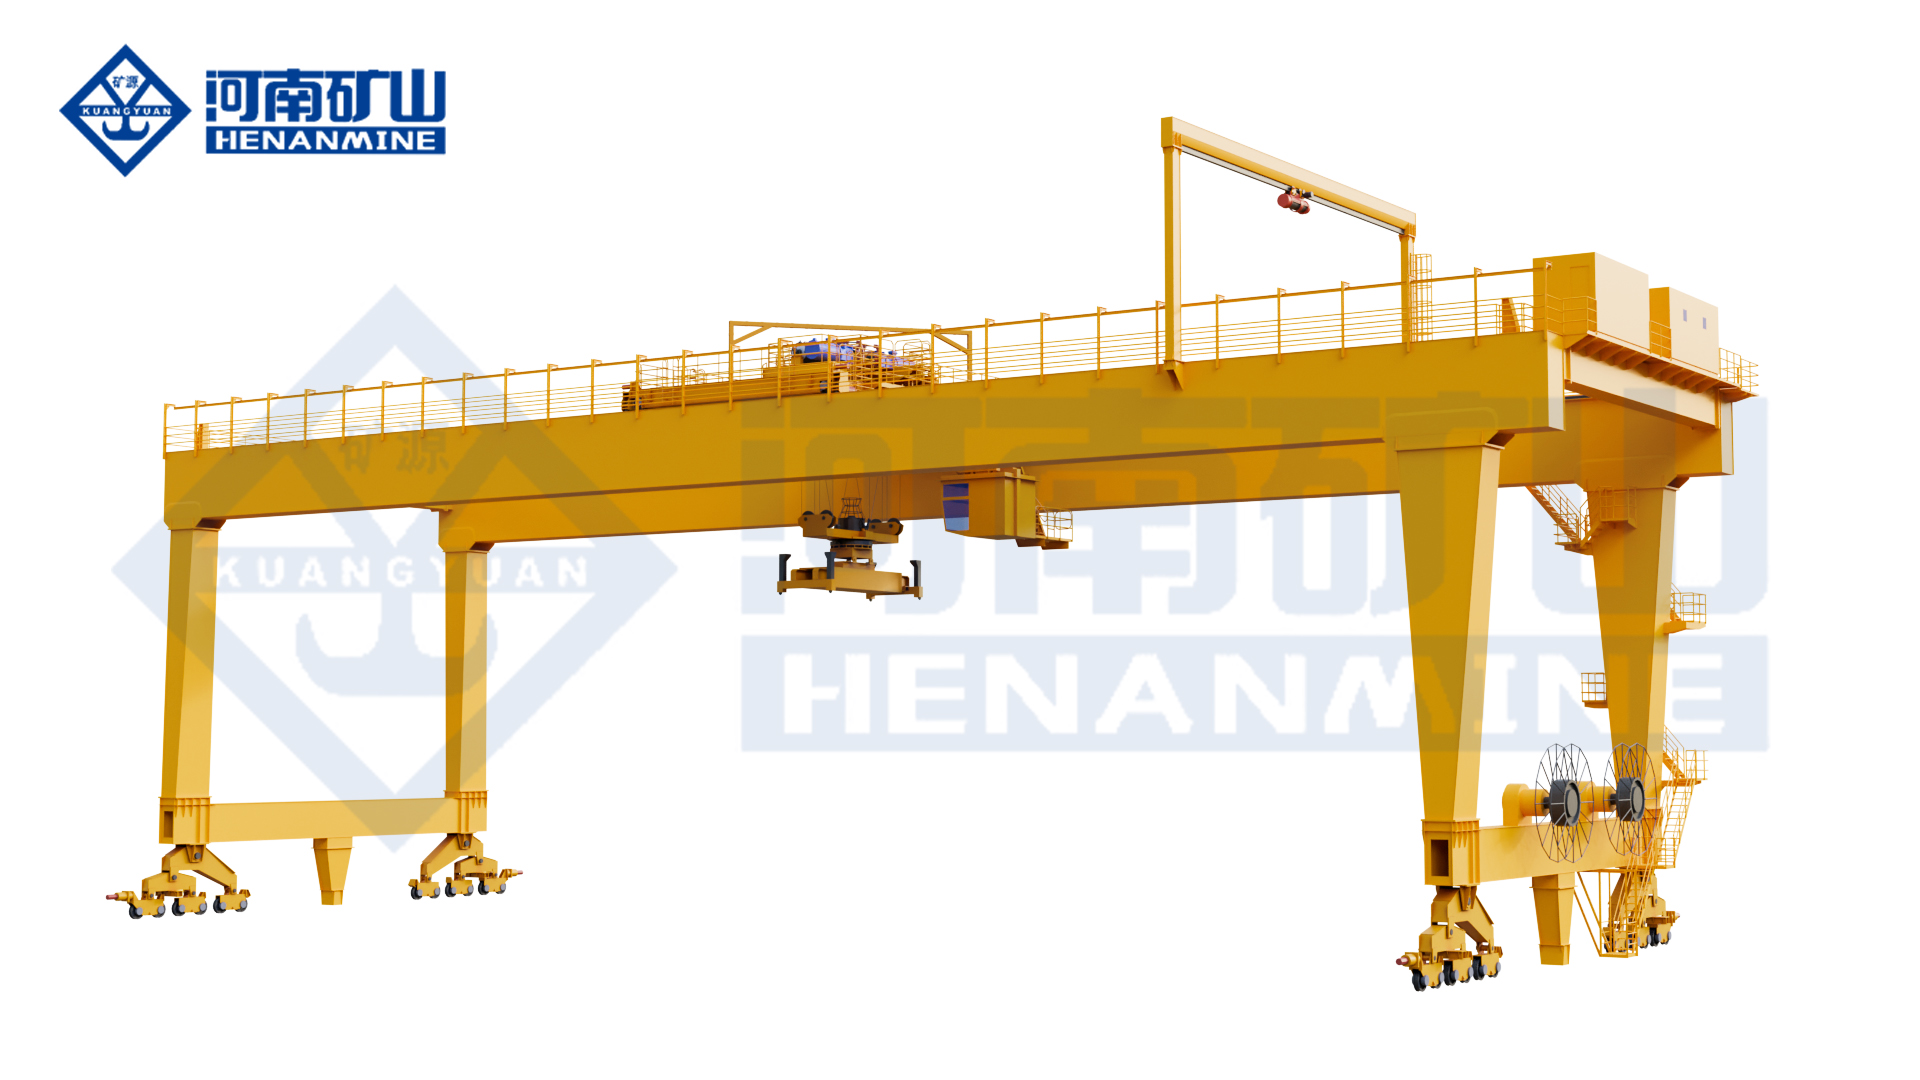
    container crane efficiency

    FAT and SAT Acceptance Test Requirements

    FAT (Factory Acceptance Test) and SAT (Site Acceptance Test) are the core mechanisms for locking in delivery quality, and the contract signing stage needs to clarify the scope of testing, acceptance criteria and responsibility:

    FAT test: carried out in the manufacturer’s factory, need to comprehensively verify the mechanical, electrical and control system functions, including lifting capacity, speed and acceleration, anti-shaking performance, emergency braking, TOS interface co-ordination and other items;

    SAT test: carried out after the equipment is installed and connected to the real environment of the port, focusing on verifying the system integration performance and operation automation rate under the actual operation scenario;

    Mandatory requirements: IEC 61508 functional safety verification is required as a mandatory sub-item of FAT and cannot be omitted.

    Software Lifecycle Cost Control

    Software life cycle cost is a hidden expenditure that is easy to be ignored, and the purchaser needs to clearly agree on the relevant responsibilities in the contract:

    • Core expenditure items: control software version upgrades, network security patches, TOS interface protocol updates, sensor calibration calibration and other ongoing cycle costs;
    • Points to be agreed: to specify the duration of software authorisation, the main body responsible for upgrading, the obligation of network security maintenance, and the time limit for responding to emergency patches; for the proprietary spreader control sub-system, it is necessary to additionally agree on the guarantee for the long-term supply of spare parts and the openness of the interface requirements.

    Key Points of Delivery Cycle Control

    Delivery cycle directly affects the project progress, and needs to be planned in advance and clearly agreed:

    Regular cycle: Standard RMG delivery cycle is 3-6 months, fully automated systems need to extend the delivery cycle due to high degree of customisation and long integration test cycle;

    Control measures: Purchasers need to reserve sufficient engineering buffer time, with clear milestone nodes and default clauses in the contract; suppliers are required to start the procurement of key long-cycle components in advance to avoid the risk of delays caused by component shortages;

    Before signing the contract, the feasibility review of the equipment transport and on-site installation plan should be completed to ensure that it matches the conditions of the port infrastructure.

    Common Misconceptions in Selection Decisions and Suggestions for Avoiding Pitfalls

    Excessive Attention to the Unit Price of Equipment

    The most common misconception in procurement is to take the unit price of equipment as the core evaluation dimension, ignoring the impact of automation system integration cost, software life cycle cost and after-sales service cost on the total life cycle cost (TCO).

    RMGs that offer low prices but have poor TOS compatibility and weak service networks often incur additional integration fees and downtime losses in actual operation that far exceed the initial price advantage, ultimately leading to a ‘low price’ solution that does not pay for itself.

    Underestimating the Complexity and Cycle Time

    When most terminals introduce automated RMG, it is easy to underestimate the difficulty and cycle of the existing TOS system transformation, and there are often problems that the existing TOS can’t support fine-grained equipment status telemetry, and can’t interact with real-time data from RMG, which leads to delayed project progress and uncontrolled cost. It is recommended to complete the TOS interface compatibility assessment before selecting the model, and include the transformation costs in the overall budget.

    Neglecting the Risk of Shortage of Composite Talents

    Automation RMG on the operation and maintenance personnel of the digital capacity requirements are much higher than traditional equipment, both know the principles of lifting machinery, but also with PLC programming, network security, AI system maintenance capabilities of the global shortage of composite talent.

    Especially in Africa, Southeast Asia and other emerging markets, this problem has become a core bottleneck restricting the return on investment in automation equipment. Purchasers need to incorporate talent training, OEM technical support, and knowledge transfer clauses into the contract to ensure stable operation and maintenance of the equipment after commissioning.

    Ignoring Supply Chain Security and Localisation Compliance Requirements

    Some regional ports RMG procurement, easy to ignore the supply chain security and local manufacturing ratio of policy constraints, especially in the U.S. market, under the influence of geopolitics and federal subsidies regulations, the local manufacturing requirements for equipment is increasingly tightened.

    Purchasers need to study the policy direction in advance, incorporate suppliers’ compliance ability into the qualification assessment, and lay out long-term equipment strategies in advance.

    Conclusion

    RMG selection is a composite decision, this paper builds a selection framework around six core dimensions: RMG and RTG fit boundary, technical specifications, automation level, TCO energy solution, safety compliance, and supplier evaluation.

    All stages of the project are recommended to start from the structured RFQ, clarify the core requirements, require suppliers to provide verifiable cases and carry out on-site research, relying on complete information to ensure that the selection decision helps port development.
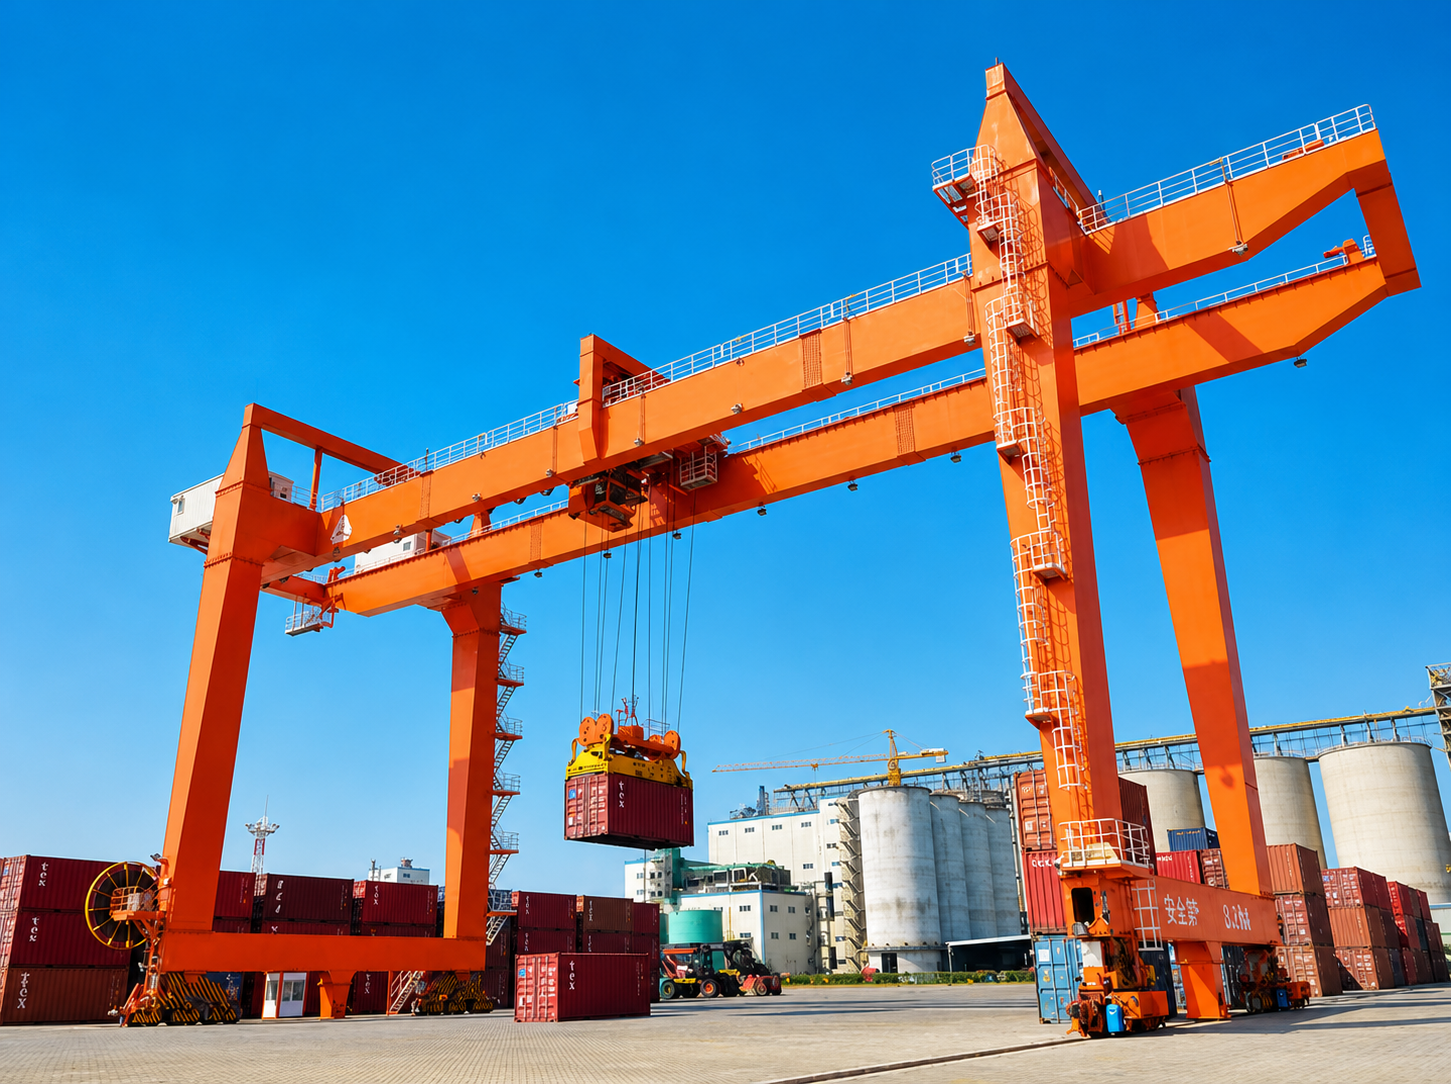
     

    Henan Mine CraneDiscuss your requirements ↗
  • How to Select a Large-Span Gantry Crane for Bridge Construction

    How to Select a Large-Span Gantry Crane for Bridge Construction

    How to Select a Large-Span Gantry Crane for Bridge Construction

    Choosing the wrong crane can be the most costly mistakes of a bridge contractor. A large-span gantry crane that is under capacity for the beam weight, or configured for the wrong erection sequence, will not simply slow the program, it can result in yard reconfiguration on the fly or a safety incident.

    Selecting a large-span gantry crane for bridge construction involves separating five related variables span, load, terrain, erection method, and regulation, from your actual project, not just the biggest number in a spec sheet.

    In this article we explain each of those five variables,  demonstrate the proper way to determine load capacity, compare each of the three key gantry variations, and highlight the terminological rules and common errors that can result in bridge equipment purchase failures.

    What Is a Large-Span Gantry Crane?

    Long-span gantry crane is self-supporting lifting equipment, using truss or box beam structure, without attachment to the building structure can achieve long-span operation.In bridge construction, portal crane and bridge erecting machine are similar in appearance, but their uses are significantly different.

    Gantry crane of beam yard is mostly used for lifting and loading transfer of beam slab of prefabricated yard; bridge erecting machine is special bridge building equipment, which can move forward by itself relying on the built pier, and directly complete the erection construction of bridge span beam section by the bridge bearing fuselage.

    Both types of equipment support single/double beam, truss/box beam structures.Truss type light weight, good wind resistance, suitable for outdoor large-span construction; box beam overall stiffness is higher, more suitable for large-tonnage heavy lifting operations.

    Key Applications in Bridge Construction

    Large-span gantry crane can be adapted to multiple construction stages of bridge engineering, equipment selection needs to be accurately matched according to the specific construction scenario, the application scenarios are as follows:

    • Transfer operation of prefabrication yard: conventional beam lifting gantry crane is used to complete the transfer operation of beam body and segment components from prefabricated pedestal to storage area or transfer equipment, which is the core equipment for standardized construction of prefabrication factory area.
    • Whole span erection construction: one-time integral hoisting and erection of whole span prefabricated beam body, mostly used for highway and railway repetitive bridge projects. This construction method can ensure the stability of the project quality, effectively reduce the on-site labor input, and improve the degree of construction standardization.
    • Segmental assembly construction: self-propelled bridge gantry crane is adopted, and prefabricated segments are assembled span by span or balanced cantilever to complete the construction of bridge span. The process is widely used in urban viaducts, curved bridges and projects with limited traffic and narrow construction space.
    • Viaduct and viaduct construction: for viaduct structure, viaduct construction scene, gantry crane can carry heavy prefabricated components along the bridge body longitudinal walking operation, adapt to the construction site space is limited, bridge line bending and other complex conditions.

    The 5-Factor Selection Framework

    Before comparing various types of crane models, a standardized SLTMS selection framework can be relied on for evaluation. The framework covers the core elements 5 span, load, site, construction method and specification, and can accurately determine the gantry crane configuration scheme of the suitable project:

    1. Span : refers to the effective operation coverage distance between the legs or piers of the equipment, which is the core parameter to determine the fuselage specifications, walking layout and overall adaptation scheme of the gantry crane.
    2. Load: Based on the actual self-weight of construction components such as beams and segments, and in combination with industry standards, the safety redundancy factor is superimposed to accurately check and approve the rated hoisting load of equipment to ensure operation safety.
    3. Site: Comprehensive evaluation of the construction site foundation bearing capacity, pier height, line curve radius and site traffic conditions, in order to match the equipment support structure and walking operation plan.
    4. Method: Combined with the established construction scheme of the project, adapt to the mainstream technology such as whole-span erection, span-by-span assembly, balanced cantilever construction, etc., and match the equipment operation mode and construction logic.
    5. Specifications (Standards): Equipment selection and operation shall strictly conform to the project territorial safety standards, industry compliance requirements and project exclusive technical specifications to ensure compliance and control throughout the construction process.

    The following will be the 5 selection of the core elements of the detailed dismantling and professional analysis.

    Matching Span Length to Crane Configuration

    Span requirements are very different from one type of crane to another and therefore getting this right at an early stage avoids the need for re-design later on.  Conventional beam-lifting and double-girder launching gantries generally have span lengths of between 20 and 50 meters and therefore will cater for most highway bridges built with pre-cast T-beam, U-beam or standard box girder segments.

    For longer spans, balanced-cantilever launching gantries can span 100m or more, as the gantry extends out from a central pier steadily,  with segments laid on each side in alternate movements, keeping the gantry in balanced condition. This type of gantry can be used for deep valleys, high piers and curved alignments which shorter span gantries are incapable of.

    Segmental launching gantries for complete suspension assembly can launch single spans of around 50 meters made with an upward-type configuration that has no constraint in pier height beneficial where the first and last line spans are constructed of piers that are lower than the whole alignment.

    Guideline: if your longest span is greater than 50m, or your alignments has very sharp curves or very irregular pier heights,  build your structure around a segmental/balanced-cantilever gantry rather than a traditional double-girder type unit.

    Calculating Load Capacity Correctly

    In the purchase of bridge erecting machine, the most common error with the biggest economic loss is the underweight type selection.General core selection standard of senior construction party in the industry: the rated lifting tonnage of equipment shall not be equal to the actual weight of the beam body, and it shall be configured according to 1.2 – 1.25 times of the actual weight of the beam body and section, so as to cover the dynamic load in lifting, slewing and positioning operations, rather than only adapting to the static lifting weight.

    144 – 150 ton bridge erecting machine shall be selected for 120 tons prefabricated beam, and 120 tons nominal equipment shall not be selected.Pure theoretical static load selection of equipment can not adapt to the dynamic construction conditions on site, easy to cause problems such as site reconstruction in the middle of construction, secondary purchase of equipment, etc., resulting in additional costs far exceeding the cost of reasonable selection in the early stage.

    The common tonnage range of different structure types of bridge erecting machine is as follows:

    • Single beam erection machine: rated tonnage 50 – 100 tons, suitable for conventional highway bridge light T beam, U beam erection construction.
    • Double-beam bridge erecting machine: rated tonnage 120 – 300 tons, suitable for medium and heavy construction scenarios, can meet the erection requirements of heavy prefabricated components.
    • Segmental erection machine: rated tonnage 700 – 900 tons, designed for large-scale box girder segmental erection projects.

    For high-precision lifting operation scenarios, the modern rail-type gantry system can realize 50 – 65 tons of double-load lifting, and the positioning accuracy can reach millimeter level; while the steel strand jack system used for complex segment construction can synchronize more than 100 lifting points.In high-precision infrastructure projects, the importance of this precise control system is no less than the rated lifting tonnage of the equipment.

    Erection Method: Full-Span vs. Span-by-Span vs. Balanced Cantilever

    Before the project lifting tonnage and equipment selection, the established bridge erection method must be determined. The construction method directly determines the type of adaptation of the gantry crane, which is the pre-core condition for equipment selection.

    • Whole span erection: the entire prefabricated bridge span is hoisted in place at one time, which is suitable for standardized repeated bridge span construction along roads and railways. The beam body is prefabricated in the controlled environment of the factory, and the construction quality is stable and reliable, which can greatly reduce the on-site operation personnel and the open-air construction process.
    • Span-by-span assembly and erection: relying on the lifting trolley on the gantry crane truss, multiple prefabricated segments are assembled into a complete bridge span. After the prestressed tensioning process is completed, the equipment is moved forward to carry out the construction of the lower 1 span. The construction method is extremely efficient, and large-scale highway projects can achieve a single-span two-day erection cycle as soon as possible, which is very suitable for projects with tight construction periods.
    • Balanced cantilever erection: take the pier as the center, extend and assemble symmetrically to both sides section by section, and maintain the structural balance during construction through bilateral alternate hoisting. This method is suitable for complex terrain conditions such as long-span bridges, curved bridges and deep valleys, and has wider applicability, but the overall construction progress is more gentle than span-by-span assembly.
    • Engineering example: Sydney western M7 highway project a total of 150 bridges, more than 2700 prefabricated segments, the project combined with the site conditions, the simultaneous use of span-by-span assembly and balanced cantilever two kinds of erection process. Large-scale infrastructure projects are usually based on bridge span parameters and site conditions, flexible with a variety of construction methods.

    Site and Terrain Assessment

    Before finalizing a gantry order, walk through the site conditions that determine whether the machine can actually operate as specified:

    • Ground bearing capacity— soft or variable subgrade may require ground improvement or a rail-mounted system to distribute load, since inadequate bearing capacity is a common cause of gantry instability.
    • Pier height variability— upward-type segmental gantries designed for self-erection at low first-and-last-span piers avoid the pier-height restrictions that trip up standard configurations.
    • Curvature and alignment— tight horizontal curves down to roughly 100-meter radii require specially hinged gantries, in some cases with up to six hydraulically regulated hinge points, to travel smoothly through the kinked sections of the girder during segment placement.
    • Access and headroom— confirm travel path clearance, working space, and whether the site is indoor, outdoor, or exposed to significant wind loading, since this affects the choice between truss and box-girder frame designs.

    Projects on deep valleys or high-pier terrain particularly favor launching gantries over ground-based cranes, because the gantry supports itself on the completed structure rather than needing stable ground access beneath every span.

    Safety Systems and Compliance Standards

    A large-span gantry crane operating over active construction zones, traffic, or waterways needs safety systems well beyond a basic overload cutoff. At minimum, evaluate whether a candidate machine includes:

    • Foundation bearing capacity: weak, uneven bearing capacity of the subgrade need to do foundation reinforcement treatment, or the use of rail-type equipment to disperse the load, the lack of foundation bearing capacity is a common cause of the instability of the bridge machine.
    • Pier height difference: the upper-mounted self-assembling segmental bridge erecting machine can be used to adapt to the low piers of the head and tail spans and avoid the pier height limit of conventional models.
    • Alignment and curvature: small curvature sections with a radius of about 100 meters of horizontal curve shall be equipped with multi-hinge hydraulic adjustment bridge erecting machine.
    • Operating space and clearance: it is necessary to verify the equipment clearance and construction operation space, and distinguish indoor and outdoor operating scenes and strong wind load environment, so as to determine the selection of truss type or box beam type fuselage structure.

    The engineering project of deep valley and high pier terrain is more suitable for bridge erecting machine operation, which is better than ground crane. The bridge erecting machine relies on the stress operation of the completed bridge structure, and does not need to have stable foundation conditions under each span, which is suitable for complex terrain construction.

    Single-Girder vs. Double-Girder vs. Segmental Launching Gantry

    Feature Single-Girder Gantry Double-Girder Gantry Segmental Launching Gantry
    Typical capacity 50–100 tonnes 120–300 tonnes 700–900 tonnes
    Typical span 20–35 meters 30–50 meters Up to 100+ meters (balanced cantilever)
    Best-fit beam type T-beam, U-beam Heavier precast beams Precast box girder segments
    Erection method Full-span, lighter loads Full-span, medium loads Span-by-span, balanced cantilever
    Structural design Light, basic frame Higher rigidity Truss or hinged, self-launching
    Ideal project type Standard highway bridges Medium-duty highway/rail bridges Long-span, curved, or high-pier viaducts
    Relative cost tier Lowest Mid-range Highest

    Buy vs. Rent and Cost/ROI Considerations

    Equipment strategy should be driven by project duration and utilization rate, not budget in advance. In general, it is stated that purchasing will be economically justified for multi-year programs with a utilization rate of approximately 60% or more, so the equipment remains in use long enough to recover investment funding. Contractors bidding on a one-off bridge for a shorter or single-span project are more likely to favor renting or initial procurement of a dedicated subcontract package.

    Consider also being prepared to look outside the sticker. Equipment purchase decisions in bridge work act as the convergence of a production and transportation and installation budget selecting an undersized gantry to minimize the initial purchase cost of a piece of equipment routinely adds the cost of downtime, safety exposure, yard rework various “industry sources estimate” that these separate factors can amount to a sum “many times” that of the remaining difference in purchase price between optimally sized and undersized equipment.

    Think of the purchase price as just one line item in the entire cost of ownership and operation, including mobilization, site preparation,  field operator training, and schedule delay costs,  if the machine does not perform as needed.

    Frequently Asked Questions

    Q: What span can a large-span gantry crane cover in bridge construction?

    Most conventional single- and double-girder gantries have spans between 20 and 50m.  Balanceds cantilever segmental launching gantries, which are over 100m have become the default option on long span or curved alignments.

    Q: How much safety margin should I add above the actual beam weight?

    Industry practice sets rated capacity at 1.2 to 1.25 times the actual beam or segment weight, accounting for dynamic loads generated during lifting and positioning rather than just static weight.

    Q: What’s the difference between a beam-lifting gantry and a launching gantry?

    A beam-lifting gantry operates in the casting yard, moving precast beams onto transporters. A launching gantry self-launches across completed piers and places segments directly into the span, supported by the bridge structure itself rather than the ground.

    Q: Can a launching gantry handle curved bridge alignments?

    Yes, if set up for it. Some special-hinged gantries a few with up to six hydraulically controlled hinges can trace curves to about 100 m radius, a typical need on an urban viaduct or LRT line.

    Q: Should I buy or rent a bridge launching gantry?

    Buying generally becomes cheaper for multi-year projects with utilization over say 60%. Shorter or single bridge projects are usually more economic with rental or a subcontracted erection package.

    Q: What safety systems should a large-span gantry crane include as standard?

    As a minimum: wind speed/direction monitoring, with automatic power cut-off, overload limiters, electrical fault protectionand mechanical safety devices such as hydraulic cylinder lock devices.

    Conclusion

    The selection of large-span gantry crane should be comprehensively judged by span, load, construction method, site, operation grade and industry specifications, not only tonnage.Accurate engineering verification in the early stage can effectively reduce risks, control costs and improve the full-cycle utilization rate of equipment.

    The working conditions of each bridge project are quite different, and the terrain, beam parameters, hoisting process and construction period requirements are different.Relying on professional lifting equipment manufacturers, we can break the limitations of general equipment and obtain customized equipment configuration solutions for project-specific working conditions.

    Henan Mine Crane can provide a full range of lifting equipment such as portal cranes and bridge erecting machines, adapt to bridge infrastructure, rail transit, port heavy industry and other scenarios, and support personalized customization.At the same time, it can provide working condition analysis, structural design, load verification and full-process technical support, and build a safe and efficient lifting operation system in one stop.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Select a Explosion-Proof Overhead Crane for Hazardous Zones

    How to Select a Explosion-Proof Overhead Crane for Hazardous Zones

    How to Select a Explosion-Proof Overhead Crane for Hazardous Zones

    Flammable and explosive gases, steam and combustible dust are common in petrochemical, pharmaceutical, grain and oil, coating and other industries.Ordinary bridge cranes are prone to electric sparks, electric arcs and high-temperature surfaces when they are running, which can easily ignite dangerous media and cause explosions and fire accidents.

    Explosion-proof bridge cranes are special equipment for high-risk working conditions. Through the structure, material, electrical and sealing explosion-proof design, the ignition risk is eliminated from the source and the safety of lifting operations in hazardous areas is guaranteed. The core advantage is the explosion-proof protection of the whole area and all parts, not the lifting tonnage.

    The key to the selection of explosion-proof cranes is that the explosion-proof grade is accurately matched with the hazardous area on the site, and the tonnage and size are for reference only.This article systematically explains the main points of a full set of explosion-proof crane selection to help enterprises comply with the selection and avoid safety risks.

    What Is an Explosion-Proof Overhead Crane

    Explosion-proof bridge cranes are special lifting equipment specially designed for hazardous environments of explosive gases, steam, and combustible dust. The whole machine has undergone explosion-proof modified design from electrical systems, mechanical components, structural materials to control systems, and can safely complete material lifting, translation, and transfer operations in designated hazardous areas, eliminating various ignition sources such as electric sparks, high temperature, and friction sparks throughout the process.

    Core anti-ignition principle

    The safety hazards of ordinary cranes are concentrated in the three dimensions of electrical sparks, mechanical high temperature, and friction static electricity, while explosion-proof cranes completely avoid risks through multiple protection mechanisms.:

    • Fully sealed explosion-proof electrical system: All electrical components such as motors, control cabinets, junction boxes, limit switches, etc. Adopt explosion-proof, increased safety, and intrinsically safe explosion-proof housings, which are completely sealed and isolated, which can accommodate sparks and arcs generated by internal short circuits, and prevent flame and high temperature leakage from igniting external explosive media.
    • Precise control of surface temperature: the surface temperature of all operating components is strictly limited to below the spontaneous combustion temperature of the on-site medium to eliminate the risk of spontaneous combustion at high temperature and adapt to dangerous working conditions of different temperature levels.
    • Anti-static and anti-friction spark design: The easy-to-friction parts are made of non-spark alloy material, and the whole machine is equipotential connected and reliably grounded to eliminate the accumulation of static electricity; the structure of the wheels, hooks, wire ropes and other components is optimized to avoid sparks from hard impact.
    • Flame-retardant and anticorrosive protection: The cable is made of thickened flame-retardant insulation material, and the equipment shell is treated with anticorrosive sealing, which is suitable for dangerous working conditions such as moisture, corrosion, and dust, so as to avoid safety hazards caused by aging and failure of components.

    Core applicable industry scenarios

    Explosion-proof bridge cranes are designed for flammable, explosive and high-risk working conditions, and are widely adapted to hazardous operating scenarios in multiple industries. The core application areas are as follows:

    • Oil and gas industry: suitable for offshore operating platforms, onshore refineries, LNG gas storage stations and oil and gas storage areas to meet the needs of equipment maintenance, pipe and material transfer operations.
    • Petrochemical and chemical industry: it covers petrochemical processing plants, fine chemical workshops, hazardous chemical production and storage plants, and is suitable for all kinds of flammable and explosive chemical media working conditions.
    • Pharmaceutical manufacturing industry: it is used in clean production workshops with combustible vapors such as API synthesis and organic solvent processing, taking into account safety and clean production standards.
    • Coating industry: suitable for high-risk environments filled with flammable and explosive volatile vapors such as painting workshops, coating and ink blending workshops, etc.
    • Dust explosion-proof industry: it can be used in grain storage and processing, wood grinding, pulverized coal treatment, plastic powder processing, etc., which are prone to combustible dust and have the risk of dust explosion.

    Understand Hazardous Zone Classification Before Selecting a Crane

    The selection of all explosion-proof cranes must be based on the on-site hazardous area classification report as the primary basis.In hazardous areas of different levels, the length of time and probability of risk of explosive media exist are different, and the corresponding explosion-proof levels and protection requirements of equipment are also very different, and they are not universal.At present, the industry uniformly divides hazardous areas into two categories: gas vapor hazardous areas and combustible dust hazardous areas.

    Gas and steam hazardous area (Zone 0/1/2)

    It is suitable for working conditions of combustible gases and volatile vapors such as oil and gas, chemical industry, coating, etc., and is graded according to the length and probability of the explosive atmosphere.:

    • Zone 0: The explosive gas/steam atmosphere persists, long-term or frequently, with the highest risk level, and the equipment is required to have the highest level of explosion-proof protection. It is mostly used in closed workshops for hazardous chemicals that continue to evaporate inside closed storage tanks.
    • Zone 1: During normal operation, there is an intermittent and occasional explosive atmosphere. It is the most common high-risk operation area in industry. Most industrial explosion-proof cranes are adapted to this area level.

    Hazardous area for burning dust (Zone 20/21/22)

    Suitable for dust conditions such as grain, wood, pulverized coal, plastic powder, etc., the dust explosion has stronger concealment and faster combustion and explosion speed. The classification standards are as follows:

    • Zone 20: Combustible dust clouds persist or frequently exist in the working space, with the highest risk, and are more common inside closed crushing and screening equipment.
    • Zone 21: There is a high probability of dust clouds during normal operation, which is the main operating hazard area of the dust factory area.
    • Zone 22: Dust clouds are generated briefly under abnormal working conditions, and the risk of daily operations is low.

    Equipment under dust conditions must meet IP6X fully sealed protection, strictly limit the surface temperature of the components, and avoid dust accumulation, heat storage, smoldering and explosion.

    The key significance of regional classification for selection

    The electrical explosion-proof level, mechanical protection standard, and temperature level of the crane must match the on-site regional level one by one.Zone 1 equipment cannot be adapted to Zone 0 high-risk environments, and dust explosion-proof equipment and gas explosion-proof equipment cannot be mixed.

    Identify the Required Explosion Protection Standard

    Explosion-proof cranes are special compliance equipment and must hold authoritative explosion-proof certification in the corresponding area. Equipment without certification, inconsistent certification, or expired certification is strictly prohibited from being put into use.The global mainstream explosion-proof certification system is divided into three categories, which are adapted to different landing areas.

    Mainstream explosion-proof certification system

    1. ATEX certification (EU standard): Mandatory access standards for the EU market, subdivided equipment protection levels, and adapted to the compliance requirements of equipment in hazardous areas throughout Europe.
    2. IECEx certification (international general standard): The most universal explosion-proof certification in the world, mutual recognition among multiple countries, suitable for cross-border projects and equipment selection in international factories.
    3. CNEX/GB certification (Chinese national standard): Mandatory compliance standards for domestic industrial projects, implemented in accordance with GB3836 series standards, all domestic explosion-proof lifting equipment must have this certification, and at the same time comply with JB/T 5897 industry-specific standards.

    Interpretation of core certification parameters

    When selecting the type, you need to focus on checking the four core parameters, which are indispensable.:

    • Explosion-proof category of equipment: Category II corresponds to the gas explosion-proof environment, and Category III corresponds to the dust explosion-proof environment. It is strictly distinguished and cannot be mixed.
    • Gas/dust category: Gas is divided into IIA, IIB, and IIC (IIC contains high-risk media such as hydrogen and acetylene, with the highest protection level); dust is divided into IIIA, IIIB, and IIIC, which are suitable for different flammable and explosive media.
    • Temperature level (T1-T6): Define the maximum surface temperature of the equipment, the highest T6 temperature level, the lowest surface temperature, and the strongest safety, which must be lower than the minimum spontaneous combustion temperature of the on-site medium.
    • Explosion-proof protection method: common explosion-proof type Ex d, increased safety type Ex e, intrinsically safe type Ex i, match the corresponding protection method according to the level of the hazardous area.

    Compliance verification requirements

    The equipment certification must match the country of the project landing and the level of the hazardous area on the site. After the selection, a professional explosion-proof engineer must verify the authenticity of the certificate and the matching of the parameters to eliminate problems such as the application of certificates, inconsistent parameters, and expired certificates.

    Determine the Required Crane Capacity and Duty Class

    The tonnage and working level of the explosion-proof crane directly determine the service life and operating safety of the equipment. Too small parameters will lead to overload, overheating, and accelerated aging of the equipment. Too large parameters increase procurement and operation and maintenance costs, which need to be accurately accounted for.

    Accurately calculate the rated lifting weight

    The selection of lifting tonnage should not only refer to the maximum material weight. It needs to be comprehensively calculated in combination with actual working conditions to fully cover static loads, dynamic loads and long-term needs:

    • Limit operating load: accurately calculate the maximum material weight on site as the upper limit of the rated lifting weight of the equipment to eliminate the risk of overload operation.
    • Auxiliary self-weight load: The self-weight of a full set of spreaders such as hooks, beams, clamps, suction cups, etc. is included in the total load calculation to avoid false marking of effective lifting weight and ensure accurate selection and compliance.
    • Normal operating load: count the conventional lifting weight of daily high-frequency operations, match the adapted crane working level, and avoid the hidden dangers of long-term light load loss or overload operation.
    • Long-term expansion margin: Combined with long-term planning such as plant capacity upgrading and equipment iteration, the lifting tonnage margin is reasonably reserved to improve the versatility and service cycle of equipment, and avoid short-term equipment elimination and repeated investment.

    Match the adapted work level

    The crane working level (A3-A8) is the core parameter that matches the frequency of operation, load strength and equipment design life, and it is also the key index for the selection of explosion-proof working conditions. The adaptation levels of different working conditions are divided as follows:

    1. A3-A4 light-level working conditions: suitable for daily short-term operation, low-frequency start-stop maintenance scenarios, mainly used for non-continuous operation scenarios such as regular maintenance of storage tanks and production equipment.
    2. A5-A6 intermediate working conditions: suitable for normal and continuous production operations in factories, and extremely versatile. It is the standard selection for mainstream explosion-proof factories such as chemical industry, grain and oil, and coating.
    3. A7-A8 heavy-duty working conditions: suitable for high-frequency, heavy-duty, and harsh working conditions of uninterrupted operation, it is widely used in high-risk continuous production lines such as oil and gas refining and chemical industry, fine heavy industry and chemical industry.

    The actual selection needs to comprehensively consider the core factors such as the daily operating time of the equipment, the frequency of start and stop per hour, and the range of load fluctuations, so as to accurately match the working level, effectively avoid the dual problems of high-configuration redundancy and waste, low-configuration overload and aging, and ensure the long-term safe and stable operation of the equipment.

    Select the Right Explosion-Proof Hoist and Electrical Components

    Explosion-proof wire rope hoist

    Explosion-proof wire rope hoist has strong bearing capacity and stable operation. It is suitable for large tonnage, large lifting height and high-frequency heavy-duty operating conditions. It is often used in double-beam explosion-proof bridge cranes and is widely used in high-intensity heavy-duty explosion-proof scenarios such as oil and gas refining and chemical industry and heavy industry.

    Explosion-proof chain hoist

    The explosion-proof chain hoist has a compact structure, a lightweight body, and a small headroom. It is suitable for small tonnage, low lifting height, and restricted plant floor height. It is often used in single-beam explosion-proof bridge cranes, which are suitable for the normal transfer of light materials in the workshop.

    Configuration of key explosion-proof electrical components

    All components of the complete electrical system must have formal explosion-proof qualifications, and the explosion-proof level is accurately matched with the hazardous area on site. The core configuration requirements are as follows:

    • Explosion-proof motor: The dual explosion-proof structure of explosion-proof and safety-enhancing is adopted, and the sealing and insulation process is used to eliminate the problem of operating sparks and overheating of components from the root cause.
    • Explosion-proof control cabinet and wiring box: an integrated fully sealed protective shell with dust-proof, explosion-proof and flame-retardant properties, which effectively blocks internal arc leakage and avoids the risk of ignition.
    • Explosion-proof limit switch and operation button: It adopts intrinsically safe explosion-proof design, with sensitive control and accurate limit, which can achieve safe and stable operation in high-risk environments.
    • Explosion-proof braking and emergency stop components: The redundant safety design of dual brakes is adopted to realize automatic self-locking of power failure, and there is no spark and no high temperature during emergency shutdown to ensure the safety of extreme working conditions.

    Evaluate Crane Structure and Layout Requirements

    The structural form and dimensional parameters of the crane need to be adapted to the plant structure and working space, otherwise there will be problems such as restricted installation, blind spots in operation, and waste of space, which will affect the stability of explosion-proof protection at the same time.

    Single beam VS double beam explosion-proof crane selection

    • High-temperature heat storage of transmission components: Bearings, gears and other transmission components operate at high frequencies for a long time. If the lubrication is insufficient, friction heat accumulation will occur, causing the surface temperature of the components to exceed the standard.
    • Explosion-proof single-beam bridge crane: compact structure, low cost, light weight, suitable for scenes with small tonnage of 1-20t, low-frequency operations, and limited net height of the plant, it is mostly used in light chemical, coating, and grain and oil workshops.
    • Hidden dangers of static electricity accumulation and discharge: The lack or failure of the grounding protection of the equipment will cause the continuous accumulation of static electricity, which will eventually cause sparks of electrostatic discharge and cause explosions.
    • Risk of overheating of the brake system: Frequent start-stop braking of the equipment will continue to generate frictional heat energy, which will cause the surface of the brake assembly to be high temperature and touch the ignition threshold of flammable and explosive media.
    • Explosion-proof double-girder bridge crane: strong bearing capacity, high stability, good fatigue resistance, suitable for 5-75t large tonnage, high-frequency heavy-duty, long-span operation scenarios, mostly used in oil and gas refining and chemical, heavy-duty chemical high-risk plants.

    Check the core layout parameters

    In the selection stage, it is necessary to accurately check the spatial layout parameters to ensure that the equipment is perfectly adapted to the working conditions of the plant, no installation interference, and no blind spots in operation. The core verification items are as follows:

    • Plant span: Refers to the distance between the center of the crane track, which determines the coverage of equipment operations.The selection needs to strictly match the span of the measured plant to ensure that the running stroke of the cart fits the working area, the equipment translation is smooth, and the problems such as operation caton and insufficient working range caused by span deviation are avoided.
    • Rated lifting height: it is the maximum safe vertical lifting stroke of the hook, which determines the vertical lifting capacity.It is necessary to combine on-site material stacking and equipment hoisting height approval, and reserve a safety margin to take into account the daily routine hoisting and large-scale components and ultra-high equipment hoisting requirements.
    • The clearance height of the workshop: it is the effective space from the load-bearing structure at the top of the workshop to the ground, which is the core restriction condition for the installation of equipment.The selection of the type needs to comprehensively consider the structural height of the main beam, hoist, limiting device, etc., and reserve a safe buffer distance to avoid interference and collision between the equipment and the plant structure.
    • End distance and hook coverage: The end distance is the safe distance from the end of the cart to the end of the track, which directly affects the coverage area of the operation.Reasonable optimization of the end distance parameters can effectively reduce the blind spots around the walls and columns, realize the global coverage of the workshop, and improve the flexibility of material transfer and operating efficiency.
    • Adaptability of track and column: The crane track needs to be accurately matched with the plant column and roof load-bearing structure to ensure smooth laying and uniform force.Compliance and adaptation can make the equipment run stably without offset and shaking, reduce mechanical wear and friction sparks, and meet the safe operation standards of explosion-proof working conditions.

    Differentiated design of indoor and outdoor working conditions

    Indoor explosion-proof cranes are designed with dust-proof, sealing and explosion-proof protection as the core design focus, and are suitable for the operating environment of closed workshops; outdoor models need to be equipped with additional windproof, rainproof, UV-resistant, anticorrosive and anti-aging protective structures to resist outdoor extreme weather erosion, protect the integrity of the explosion-proof structure of the equipment in all directions, and ensure long-term safe and compliant operation.

    Review Safety Features and Control Systems

    Qualified explosion-proof bridge cranes must be equipped with a full set of redundant safety protection devices to realize fault self-inspection, active protection, emergency risk avoidance, and avoid the risks of dangerous working conditions in all directions.

    Essential basic safety equipment

    • Overload protection device: equipped with a high-precision load detection module, it can instantly sound and light alarm and lock the lifting action when it is overloaded, effectively avoiding component deformation, motor overheating, wire rope fracture and other failures, and eliminating the hidden dangers of explosion under high-risk working conditions.
    • Upper and lower limit and walking limit devices: equipped with explosion-proof limit switches to accurately limit the lifting of the hook and the walking stroke of the equipment, prevent problems such as rushing to the top, falling to the bottom, and offside collisions, and avoid ignition sparks caused by mechanical impact and friction.
    • Fail-safe brakes: The redundant design of power-off self-locking is adopted, and the braking is stable during normal operation. The load can be instantly locked in the event of sudden power failure or failure, so as to prevent safety accidents such as sliding hooks, sliding cars, and falling heavy objects.
    • Multi-point explosion-proof emergency stop device: Intrinsically safe explosion-proof emergency stop buttons are set in multiple places on the fuselage and operation console. In emergency conditions, one-button power-off and shutdown can be turned off and all actions can be locked, and the loss can be stopped quickly to prevent the accident from expanding.
    • Anti-collision system: suitable for multi-machine operation scenarios on the same track, real-time monitoring of equipment spacing through explosion-proof infrared induction, automatic deceleration, early warning and shutdown at close range, to avoid friction sparks and high temperature caused by equipment collisions, and to ensure explosion-proof and safe production in intensive workshops.

    Intelligent adaptation configuration

    The frequency conversion speed control system (VFD) needs to adopt an explosion-proof sealed cabinet to achieve smooth start and stop, accurate positioning, and avoid component friction sparks caused by impact loads; it is equipped with an intelligent monitoring system, which can monitor the temperature, load, operating frequency, and fault code of the equipment in real time to achieve preventive operation and maintenance, and does not destroy the equipment’s explosion-proof certification compliance throughout the process.

    How to Choose a Reliable Explosion-Proof Crane Manufacturer

    The core of equipment selection depends on parameter matching and half on the strength of manufacturers. High-quality manufacturers are the guarantee of equipment safety, compliance and long-term stable operation. The selection of manufacturers needs to focus on 7 dimensions of verification.:

    1. Industry-specific experience: deeply engaged in high-risk industries such as oil and gas, fine chemicals, dust explosion-proof, etc., has rich experience in on-site project implementation, and is familiar with the compliance norms, working conditions, pain points and safety selection standards of various hazardous areas.
    2. Customized R&D capabilities: With exclusive program R&D and design capabilities, it can be customized on demand according to plant space parameters, operating frequency, explosion-proof level and on-site environmental conditions, and can be applied to general models to meet the needs of personalized high-risk working conditions.
    3. A full set of compliance certification: The manufacturer has complete qualifications and compliance. The whole machine and the core components such as motors, hoists, and electrical components all hold valid and traceable explosion-proof certifications. The parameters are accurately matched with the working conditions to eliminate hidden compliance risks such as certification, expiration, and undocumented.
    4. Complete technical data output: A full set of compliance technical data can be provided, including equipment drawings, factory inspection reports, explosion-proof qualification certificates, operation and maintenance manuals, etc., which fully meet the requirements of equipment acceptance, annual inspection and safety production verification.
    5. Strict quality inspection system: establish a standardized factory quality inspection process, and strictly complete all tests such as load performance testing, electrical explosion-proof testing, and safety function verification before the whole machine leaves the factory, so as to prevent the delivery of unqualified equipment from the source.
    6. Perfect after-sales guarantee: equipped with a one-stop after-sales service system, covering professional installation and commissioning, operator skills training, regular inspection and maintenance, original factory certified parts supply and other services to ensure the long-term safety, compliance and stable operation of equipment.
    7. Design ability to adapt to all working conditions: it can accurately match customized design plans for different lifting tonnage, plant span, work level, explosion-proof level and complex environmental working conditions, and adapt to various high-risk production scenarios.

    Conclusion

    The selection of explosion-proof bridge cranes cannot only depend on tonnage and price, but must be combined with on-site explosion-proof grade, media characteristics, working condition parameters, compliance, and operation and maintenance requirements for comprehensive selection.Enterprise procurement should abandon the misunderstanding of low prices, verify the explosion-proof qualification of equipment, configuration quality and the technical capabilities of manufacturers, accurately match working conditions, avoid safety risks, and control full-cycle costs.

    Henan Mine Crane can provide explosion-proof bridge cranes and customized solutions for hazardous environments such as petroleum, chemical industry, and natural gas. It is tailored according to on-site explosion-proof requirements, working conditions and plant conditions to balance safety, reliability and economy to ensure safe production under hazardous working conditions.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Select a Crane for Foundries and High-Temperature Industrial Environments

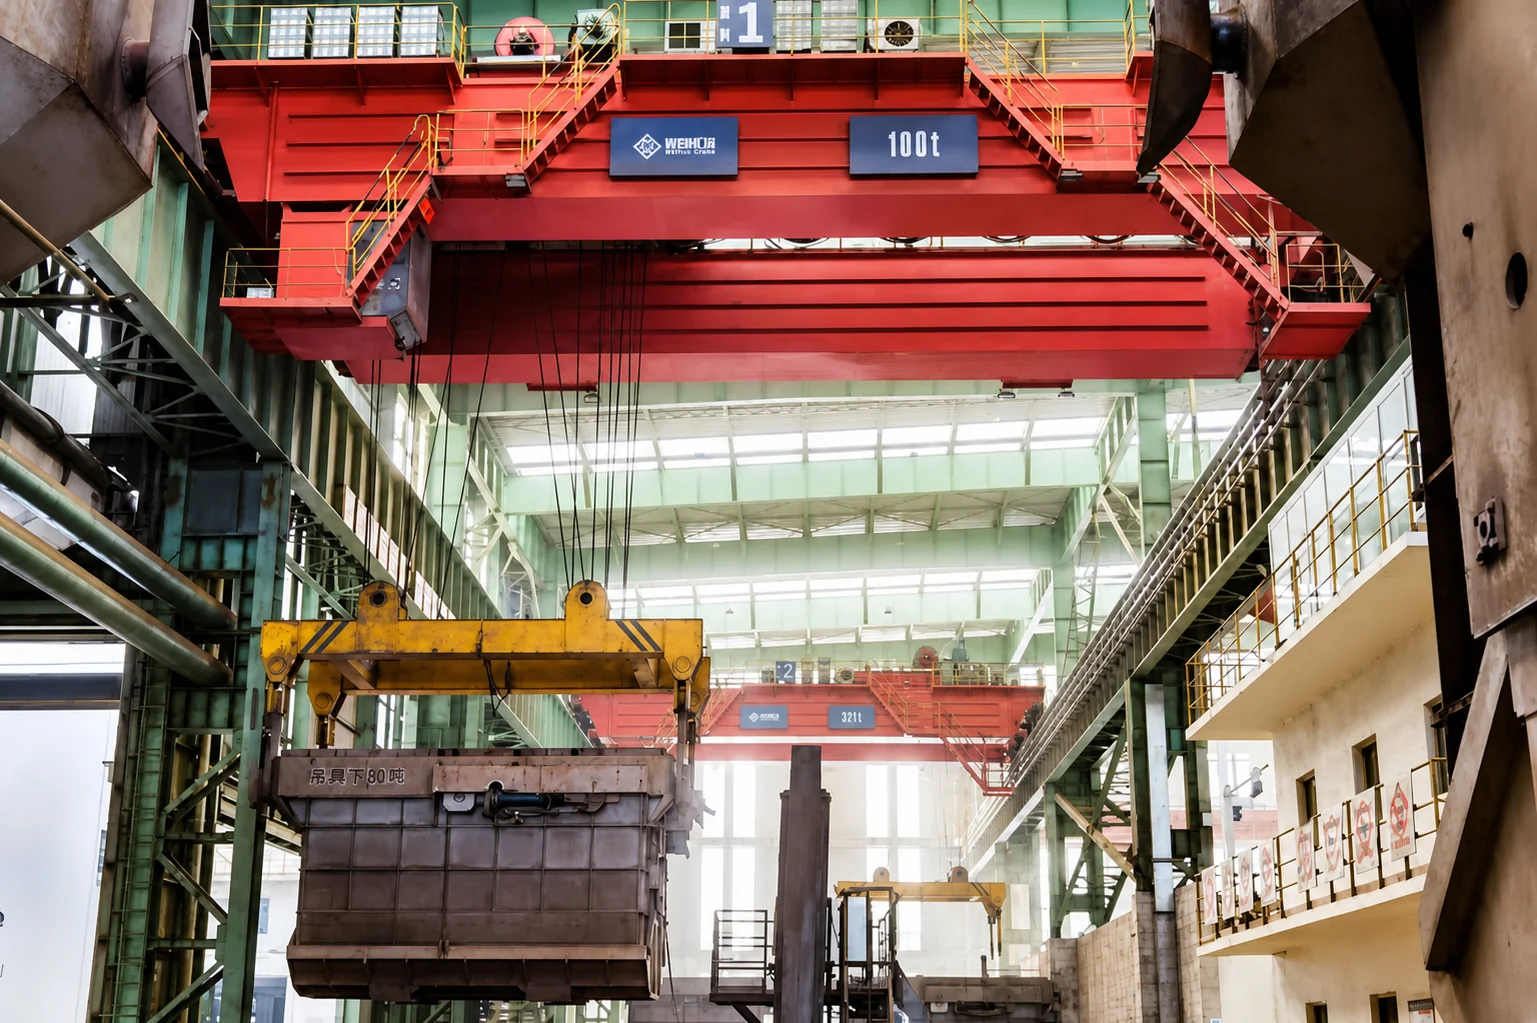
    How to Select a Crane for Foundries and High-Temperature Industrial Environments

    How to Select a Crane for Foundries and High-Temperature Industrial Environments

    The foundry workshop and the high-temperature industrial environment put forward higher requirements for the heat resistance, carrying capacity and operating stability of the Henan Mine Crane Factory supply crane.Continuous thermal radiation, metal dust and frequent heavy-duty operations will accelerate the aging of key components and increase equipment failure and safety risks.To choose a suitable casting crane, it is necessary to conduct a comprehensive assessment based on actual working conditions, load parameters, working level, thermal protection configuration and equipment maintenance requirements to ensure that the lifting equipment adapts to the production environment, while ensuring the safety of hoisting and operating reliability, reduce unplanned downtime and long-term operating costs.

    Why Foundries Need Specialized Industrial Cranes

    Radiant heat exposure

    The core working condition challenge of the foundry workshop is continuous strong thermal radiation. Molten metal ladles and smelting furnaces will radiate hundreds of degrees Celsius of heat energy, which is not simply environmental high temperature.The heat will continue to bake the main beam of the crane, trolley, wire rope, motor, and electrical cabinet, accelerating the aging of the paint, the decline in the strength of the metal material, and the brittleness of the cable insulation layer.The failure rate of the electrical and transmission components of ordinary cranes will increase exponentially under long-term thermal radiation.Even if it is far away from the bath, intermittent thermal shock in the operating area will shorten the life of the whole machine. Therefore, the casting crane must be specially designed for thermal insulation, and the normal temperature workshop crane scheme cannot be directly applied.

    Heavy loads and molten metal

    The casting crane undertakes the transportation of molten metals such as molten steel, molten iron, and molten aluminum. The load is not only static weight, but also includes the weight of the ladle and the dynamic impact load caused by the shaking of the liquid metal.Molten metal is a high-risk load, and once the spreader and lifting mechanism fail, it will cause a serious safety accident.The equipment must not only meet the rated load, but also need redundant safety braking and anti-overturning spreader structure.Conventional cranes have insufficient safety redundancy and are not suitable for liquid metal hoisting. From the structural design of the special crane for casting, it provides multiple protections against impact loads and the risk of liquid metal leakage to ensure stable and controllable heavy-duty transportation.

    Harsh operating conditions

    In addition to high-temperature thermal radiation, the foundry workshop is also accompanied by a large amount of metal dust, oxidized soot, splashing metal debris, and corrosive fumes in some scenes.Dust can easily invade bearings, gears, brakes, and electrical contacts, causing wear, stagnation, and short circuits.The crane needs to continue to operate in a dusty, vibrating, and high temperature splash environment. The sealing and wear resistance of ordinary models are insufficient, and the mechanism will be stuck and electrical failures will occur in a short period of time.The special casting crane optimizes the sealing and wear-resistant structure of the whole machine, improves the splash resistance, maintains stable operation under harsh working conditions, reduces sudden downtime, and guarantees the continuous production of the casting production line.

    Common Crane Types for Foundries and High-Temperature Applications

    Foundry overhead cranes

    The foundry bridge crane is the main model with the most extensive application range in the foundry workshop. It adopts a double-beam or four-beam structure and is suitable for high-temperature cross-operation such as smelting, casting, and ingot transfer.The structure of the whole machine is stronger, equipped with thermal insulation protection and dual braking safety system, and the working level generally reaches the A7/A8 extra-heavy level, which can withstand thermal radiation and frequent start and stop for a long time.This model runs along the top track of the plant and does not occupy ground space. It is suitable for the transfer of materials, hot blanks, and empty ladles in large and medium-sized foundry workshops.According to the workshop span, lifting height and thermal radiation level, thermal insulation guards and high-temperature electrical systems can be customized to adapt to most casting high-temperature working conditions.

    Ladle handling cranes

    Ladle/ladle crane is specially used for the lifting, transshipment, and alignment of molten metal ladles. It is a high-risk core process equipment in the foundry workshop.The equipment comes standard with a fixed gantry hook structure to withstand the huge load of ladles and molten metal. The lifting mechanism is equipped with two sets of independent braking systems, which have load monitoring and early warning functions for the tilt of the package body.This type of crane has the highest requirements for safety and redundancy, and can complete the liquid metal transportation from the furnace to the casting station, covering steel and non-ferrous metal casting scenes.All key metal components, wire ropes, and electrical components are selected with high temperature resistant models to cope with close-range and strong thermal radiation environments.

    Charging and casting cranes

    The feeding and casting crane is mainly responsible for feeding the smelting furnace and the precise casting of liquid metal in the casting station, taking into account the needs of heavy-duty lifting and high-precision alignment.Under feeding conditions, the material impact is large, and the casting process requires low speed and stability to prevent the liquid metal from shaking and overflowing.The lifting speed of this model is adjustable, and the micro-motion control performance of the trolley is strong, and it can cooperate with the production line to complete the complete process of feeding, slag removal, and casting.The equipment structure strengthens thermal insulation protection against close-range thermal radiation in the furnace mouth area, while optimizing the operation response, which is convenient for operators to control the dumping of ladles and the flow of liquid metal. It is widely used in continuous casting and mold casting production lines.

    Key Factors to Consider When Selecting a Foundry Crane

    Load capacity and workshop layout

    The first step in the selection is to calculate the maximum load. All the weight of the ladle, the weight of the molten metal, and the weight of the spreader must be included, and a safety margin must be reserved. It cannot be simply matched according to the nominal tonnage of the product.At the same time, it is necessary to map the span of the plant, the height of the rail top, the position of the column, the workshop passage, the layout of the furnace and the casting station.The restricted space needs to optimize the contour of the trolley to avoid obstacles such as the steel structure and furnace body of the plant.It is also necessary to plan the operation route of the cart and reserve a safe passage for the transfer of molten metal.Combine the layout of the workshop to determine the crane span, lifting height, and buffer limit scheme to ensure sufficient space for equipment installation, operation, and maintenance.

    Duty class and operating frequency

    The working level is the core index that can be easily ignored in the selection of casting cranes, and ordinary A3-A5 light and intermediate cranes cannot be used for continuous casting operations.The foundry hoists molten metal, with frequent start and stop, and large load fluctuations. The mainstream selection of A7 and A8 special heavy work grades.It is necessary to count the number of daily cycles, the length of a single job, and the ratio of no-load and heavy-load alternation to determine the level of work.If the working level is selected to be low, the mechanism, gear, and wire rope will be overloaded and tired for a long time, and the risk of metal fatigue and fracture will quickly occur.Only by matching the correct working level can the life of the equipment be extended and the probability of major failures be reduced.

    Lifting speed and positioning accuracy

    The lifting speed and positioning accuracy requirements of different casting processes are obviously different. When transporting molten metal, it is necessary to be stable at low speed to suppress liquid shaking.The speed of feeding and transferring the billet can be appropriately increased to ensure production efficiency.The casting station requires precise micro-motion control to achieve precise alignment of the ladles.When selecting the model, confirm the speed regulation scheme of the lifting mechanism, check the micro-motion capacity of the trolley, and take into account the operating efficiency and safety.Too fast speed will cause the metal liquid to shake violently, which will increase safety risks.If the accuracy is insufficient, the pass rate of the finished product will decrease.Professional manufacturers can customize the speed regulation range and positioning control scheme according to process requirements.

    Molten metal handling requirements

    There are mandatory special requirements for cranes lifting molten metal. Fixed gantry hooks are preferred for spreaders. The lifting mechanism must be equipped with a dual independent braking system, real-time monitoring of the loading load, and an alarm device for the tilt of the package body.It is necessary to distinguish different metals such as molten steel, molten iron, and liquid aluminum, corresponding to different temperature levels and splash protection schemes.At the same time, plan the emergency response design, such as keeping the load from falling in a fault state.Ordinary heavy-duty cranes cannot be retrofitted for liquid metal lifting.All structures, spreaders, and safety components must comply with the relevant safety regulations for molten metal hoisting and meet the requirements of supervision and inspection.

    Heat Protection and Safety Requirements for Foundry Cranes

    Heat shields and insulation

    Heat insulation panels and heat shields are the most basic protective means to isolate the thermal radiation of the ladle. High-temperature-resistant heat insulation panels are installed at the bottom of the main beam, the bottom of the trolley, and the electrical box to block the direct baking of metal structures and electrical components by radiant heat.The selection of insulation materials needs to withstand continuous high temperature and resist metal splashing and burning, while taking into account the lightweight structure to avoid increasing the weight of the crane.According to the distance of the working area from the bath, different thermal radiation levels are divided, and the thickness and structure of the heat insulation board are adjusted.The thermal insulation system needs to reserve space for maintenance, regularly check the deformation and burning conditions, and replace the damaged thermal insulation parts in time to maintain the protective effect.

    Heat-resistant components

    Ordinary wire ropes, motors, cables, and seals will fail quickly in high temperature environments, and Henan Mine Crane Factory supply casting cranes must choose a full set of high temperature resistant supporting components.High-temperature resistant steel wire ropes, metallurgical special motors, high-temperature resistant special cables, and high-temperature greases can maintain material properties in a continuous thermal environment.Bearings, gears, pulleys and other transmission components should also be upgraded to improve wear resistance and strength at high temperatures.The selection of parts and components should not only look at the nominal temperature, but also consider the long-term thermal cycle aging effect.All accessories of the whole machine close to the high temperature area need to be tested under high temperature conditions to ensure long-term stable operation.

    foundry crane

    Braking and overload protection

    In the case of molten metal hoisting, the braking system is the bottom line of safety. The casting crane adopts a redundant design of dual brakes. The main brake and the safety brake are independent of each other, and the load can still be locked if a single brake fails.The equipment integrates an overload protection device to monitor the lifting load in real time, automatically cut off the lifting action and trigger an alarm when it is overloaded.At the same time, limit limits and cushioning devices are configured to prevent over-stroke collisions between large cars and small cars.The system can collect the status of the brake in real time and give early warning of brake pad wear.Multiple protection linkage, to avoid the risk of falling packages caused by overload and mechanism failure, and to meet the mandatory safety requirements of metallurgical casting scenarios.

    Operator protection and remote controls

    Traditional cab operation will expose the operator to high temperature, strong light, and metal splashing for a long time. Modern foundry cranes provide heat-insulated and air-tight cabs or wireless remote control systems.The heat-insulated cab is equipped with a heat-insulating layer, shading protection, cooling and ventilation to isolate high temperature and thermal radiation.The remote control scheme can place the operator in a safe area away from the bath to operate, reducing the risk of personal injury.The remote control system needs to ensure stable signal, low latency, and emergency stop function.Enterprises can combine the layout of the workshop, choose the dual modes of cab and remote control, take into account the operating vision and personnel safety, and adapt to different casting processes.

    Applicable safety standards

    Casting high-temperature cranes must comply with the lifting and metallurgical safety regulations corresponding to the domestic and export target markets, and the domestic requirements such as TSG 51 lifting machinery safety technical regulations and molten metal lifting safety regulations must be met.From design, materials, manufacturing, factory testing to on-site installation and acceptance, every link must be benchmarked to corresponding standards, and reports on flaw detection, load testing, and high temperature testing must be kept.Export projects need to match local industry safety regulations.At the procurement stage, it is necessary to confirm whether the manufacturer designs and produces in accordance with the corresponding standards, and the equipment acceptance and annual inspection also need to comply with the specifications to avoid compliance risks and safety risks.

    How to Evaluate Foundry Crane Manufacturers

    High-temperature project experience

    Evaluation manufacturers first investigate the landing cases of high-temperature casting projects, and give priority to manufacturers with a large number of metallurgical and non-ferrous metal casting crane delivery experience.Ordinary crane manufacturers are familiar with hoisting factories at room temperature, but they lack project experience in molten metal hoisting and strong thermal radiation conditions, and they have insufficient understanding of thermal deformation, dust protection, and safety redundancy design of molten metal.Manufacturers are required to provide project cases of the same tonnage, the same conditions, on-site real shots, and customer feedback to understand the long-term operating performance of the equipment.Mature manufacturers can predict various potential problems in high temperature operating conditions and avoid risks in advance during the program phase.

    Custom engineering and testing

    The working conditions of the foundry workshop are extremely differentiated, and there are few fully standardized equipment, which requires manufacturers to provide customized engineering design services.Professional manufacturers will survey the working conditions of the workshop on the spot, do thermal environment assessment, load simulation, structural finite element analysis, and adjust the main beam, heat insulation, electronic control, and spreader plans in a targeted manner.Before the equipment leaves the factory, it needs to complete the full load test, brake performance test, and high temperature simulation test, and issue a complete test report.It is necessary to refuse to do only simple re-marking of standardized cranes, customized design capabilities and rigorous factory testing are the key to ensuring that casting cranes are adapted to high-temperature and high-risk working conditions.

    Maintenance and technical support

    Henan Mine Crane Factory supply Casting cranes are high-risk special equipment, and the late maintenance capacity directly determines the length of downtime and safety level of the production line.When evaluating suppliers, confirm the localized technical team, spare parts warehousing, emergency response timeliness, and regular inspections, non-destructive testing, and annual inspection assistance services.Wearing parts are lost faster in high temperature environments, and the supply of original spare parts needs to be stabilized.Excellent manufacturers can provide remote equipment condition monitoring, predict component aging in advance, and carry out preventive maintenance.A perfect technical support system can shorten the downtime, reduce the probability of sudden accidents, and ensure the continuous operation of the casting production line.

    Lifecycle cost comparison

    Many purchases only compare the unit price of equipment purchases, ignoring the whole life cycle cost.The comprehensive cost of casting cranes includes purchase price, installation fee, annual inspection fee, replacement of spare parts, maintenance working hours, energy consumption, and loss of downtime.Low-cost equipment often simplifies heat insulation, braking, and material configuration. The failure rate is high in the later stage, the replacement of spare parts is frequent, and the loss of production is huge.During the evaluation, it is necessary to account for all costs within a 5- to 10-year cycle, and comprehensively compare equipment reliability, maintenance costs, and expected service life.The early investment of high-quality casting cranes is higher, but there are fewer failures, lower long-term comprehensive costs and stronger safety.

    Common Mistakes to Avoid When Buying a Foundry Crane

    Underestimating heat exposure

    The most common selection misunderstanding is to underestimate the impact of thermal radiation, only refer to the ambient temperature of the workshop, and ignore the thermal shock of the short-range radiation of the ladle.The purchasing staff believes that the air temperature in the workshop is not high, so they directly choose ordinary bridge cranes without increasing heat insulation protection.After the equipment is put into use, the main beam, electrical cabinet, and cables continue to be heated, and insulation aging, structural deformation, and frequent tripping repairs occur in the short term.Thermal radiation is not continuous and constant, and instantaneous high temperature shocks will occur when the liquid metal is dumped and close to the furnace body.In the selection stage, the maximum thermal radiation intensity must be evaluated on the spot, and sufficient thermal insulation and protection design margin must be reserved.

    Choosing the wrong duty class

    The low selection of work level is a major safety hazard in the foundry workshop. In order to save budget, some purchases use A5 and A6 grade cranes to undertake high-frequency molten metal hoisting.The structure and transmission mechanism of this kind of equipment are designed according to a medium load cycle, and cannot withstand a large number of daily start-stop and alternating loads in the foundry workshop.After being put into production, the wire ropes, gears, and wheels quickly fatigue and wear, greatly increasing the risk of structural fracture.The work level cannot be judged by the rated load, but must be determined based on the daily work cycle and load spectrum.Rather, the selection margin is too large, and the work level must not be downgraded to drive down costs.

    Overlooking safety requirements

    Many purchases focus on load and price, ignoring the mandatory safety provisions for molten metal hoisting, and omitting safety configurations such as double braking, load monitoring, and gantry hooks.Some enterprises purchase ordinary cranes and retrofit their own spreaders for molten steel transfer, which is a major safety hazard and cannot pass the inspection of special equipment.Safety configuration cannot be regarded as an optional value-added item, and the safety redundancy of molten metal hoisting is a hard requirement.In the early stage of procurement, it is necessary to sort out the safety list, check the equipment configuration item by item, refuse to delete the safety components, and avoid huge losses caused by later rectification, shutdown, and safety accidents.

    Focusing only on purchase price

    The simple price comparison is to purchase high-frequency pit-stepping points. Low-cost casting cranes often use methods such as thinning the main beam steel plate, downgrading high-temperature accessories, and simplifying brake protection to compress costs.Short-term procurement costs have fallen, but the equipment failure rate has soared, and the loss of spare parts replacement and shutdown has continued to increase.In the event of a safety accident, the loss is incalculable.Procurement decisions should integrate safety level, equipment life, maintenance costs, and supplier service capabilities.Take the purchase price as one of the reference indicators, not the only judgment criterion, and choose a safe and reliable solution with better economy throughout the life cycle.

    Henan Mine Crane Factory Custom

    The selection of cranes in foundries and high-temperature industrial environments requires comprehensive consideration of complex working conditions such as thermal radiation, molten metal lifting, heavy-duty and high-frequency operations, and dust.From lifting weight, working level to thermal protection and safety configuration, every parameter is related to production efficiency, equipment reliability and on-site operation safety.Choosing a suitable casting crane must not only meet the current hoisting needs, but also take into account the workshop layout, production cycle and long-term maintenance costs to avoid frequent downtime or subsequent retrofits due to improper selection.

    Henan Mine Crane provides lifting equipment for metallurgical, casting and heavy industrial scenarios, including double-girder casting cranes, four-girder casting cranes and metallurgical bridge cranes. Corresponding plans can be formulated according to the load requirements, operating conditions and on-site conditions of the project.Whether it is molten metal transfer, pouring operations, or heavy-duty material handling in high-temperature workshops, professional engineering design and reasonable equipment configuration can provide strong support for production and operation.If you are planning to build a new foundry or upgrade an existing hoisting system, you are welcome to contact the Henan Mine Crane team to communicate project parameters and customized requirements to obtain crane solutions that are more suitable for actual working conditions.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Reduce Port Crane Downtime in High-Traffic Terminals

    How to Reduce Port Crane Downtime in High-Traffic Terminals

    How to Reduce Port Crane Downtime in High-Traffic Terminals

    Global freight volume continues to rise, high-flow container terminals shore bridge (STS), tire gantry cranes (RTG) as the core loading and unloading equipment, once the unplanned downtime, far from only generating maintenance costs, but also triggered a chain of crises throughout the terminal operation.

    Ship stranded, berth turnover obstruction, demurrage soaring, cargo throughput decline, direct loss of competitiveness of the terminal industry and customer trust, in the fast-paced global trade, crane idle every minute, are real economic losses and efficiency losses.

    Many terminal managers fall into a misunderstanding: that speed up the maintenance speed can solve the problem of crane downtime, but in fact, passive repair can only treat the symptoms, can not be curbed from the root cause of the risk of downtime.

    Want to really reduce the high-flow terminal crane downtime, the core lies in the transformation of operational thinking, from passive maintenance to active prevention and control, relying on systematic root cause investigation, prospective maintenance, intelligent technology landing, resource optimization and professional team building.

    Core Causes of Port Crane Downtime in High-traffic Terminals

    Compared to ordinary terminals, cranes in high-flow ports are in an overloaded state, and the risk of downtime is infinitely amplified, and the core driving factors are mainly divided into four categories:

    1. the equipment long-term high load operation, minor faults are very easy to quickly evolve into major failures;
    2. the terminal of all aspects of operation linkage, yard scheduling, ship scheduling, collector card diversion, and so on any part of the inefficiency, will aggravate the crane wear and tear;
    3. the lack of systematic equipment operation and maintenance, heavy maintenance and light prevention;
    4. human operation, environmental erosion and other external factors superimposed to further enhance the probability of failure.

    Identify and Address Root Causes of Downtime

    Build a systematic root cause analysis (RCA) system. To solve the problem of crane downtime, do not rush to repair, you need to carry out professional root cause analysis first, jump out of the surface maintenance misunderstanding. Terminals should establish a complete fault ledger, integrated inspection, operation and maintenance data, combined with the frequency of operation, peak and other operational data, digging deep into the core causes of failure.

    For example, if the wire rope breaks frequently, you can’t just replace the parts, you need to trace the operation, maintenance, parts wear and tear and other deeper problems to prevent the recurrence of the same kind of failure.

    Combined with industry operation and maintenance data, high-flow quay crane unplanned downtime, mainly from five core issues, corresponding to different prevention and control direction:

    Mechanical and Structural Failures

    Henan Mine Crane Port Crane

    Electrical and Control System Issues

    automated, semi-automated shore bridge and gantry crane core failure point, high-flow terminal operating rhythm, electrical components, PLC controller, all kinds of sensors for a long time high-frequency start-stop operation, very easy to fail, false alarms, coupled with the port of the open-air environment, line aging, short-circuiting moisture, unstable power supply voltage problems, will trigger equipment Sudden shutdown.

    These faults are hidden faults, difficult to investigate high professional requirements, ordinary operation and maintenance personnel are difficult to quickly locate the problem, often significantly lengthen the maintenance time, further aggravating the terminal operation congestion.

    Human Errors and Operational Inefficiencies

    completely preventable but high incidence of downtime triggers, part of the terminal in order to catch up with the operating schedule, appointed without a license, without systematic training of the operator, the operation of the existence of diagonal pulling and slanting crane, over-speed lifting, illegal steering, and other irregularities in the operation, or go to work before the inspection is perfunctory, omission of checking the wire rope wire breakage, brake loosening and other minor hazards, the long-term down will be directly damaged!

    Crane core components, significantly shorten the service life of the equipment, and even instantly triggered equipment failure and safety accidents, is the most easy to ignore the high-flow terminal but the impact of great downtime factors.

    Severe Environmental Erosion

    coastal high-flow terminals are unique to the high incidence of hidden danger, high air salt content in the harbor area, high humidity, coupled with extreme temperature differences, strong winds and heavy rains and other inclement weather, the salt spray will quickly corrode the crane metal steel structure, fasteners and electrical wiring shells, resulting in short circuits, corrosion problems.

    At the same time, high or low temperature environment will accelerate grease failure, thermal expansion and contraction of components deformation, continue to aggravate the aging speed of the equipment, so that the original durable components fail in advance, significantly increasing the probability of unplanned downtime.

    Importance of Root cause Analysis (RCA)

    Indirectly induced crane downtime of the core operational issues, high-flow terminals, if the yard planning chaos, container stacking disorder, unreasonable ship scheduling, truck scheduling lag, will lead to cranes are forced to frequent idling, long-distance walking, repeated inverted box handling, additional increase in equipment operating load and frequency of operation.

    The original loading and unloading can be completed at a time, it takes Multiple operations to complete, not only a waste of operating time, but also accelerate the wear and tear of components, so that the crane is in a long-term fatigue state, and ultimately induced all kinds of mechanical and electrical failures, forming a vicious cycle of operational inefficiency and equipment downtime.

    Adopt Predictive & Preventive Maintenance Strategies

    Preventive maintenance is the basis for downtime, in strict accordance with the original equipment (OEM) standards, the development of normalized grading maintenance plan, low-cost routine maintenance, to avoid high amounts of overhaul downtime, and put an end to equipment with sick operation. High-flow terminals need to be graded according to component maintenance: daily inspection of the core checking wire rope, brake and other key parts;

    weekly and monthly maintenance focus on lubrication, fastening and line inspection; annual steel structure flaw detection, core component overhaul and other in-depth maintenance. Strictly adhere to the original specifications, timely handling of minor faults, with professional operation and maintenance team, to ensure the effectiveness of maintenance.

    Predictive maintenance is more suitable for high-intensity operation of high-traffic terminals, relying on the real-time operation data of equipment to predict failures and realize accurate operation and maintenance, avoiding excessive maintenance and eliminating unplanned downtime.

    Henan Mine Crane Port Crane

    The terminal can collect core data such as operating hours and component status through sensors to build a big data early warning model, which automatically warns of data anomalies and allows the O&M team to overhaul the equipment in advance without affecting normal operations. This data-driven model can improve the efficiency of operation and maintenance, promote maintenance from passive repair to active prediction, is the core means to improve the reliability of cranes.

    Leverage Smart Technologies and Automation

    Intelligent Transformation of Old Equipment

    Old cranes do not need to blindly replace the entire machine, priority upgrade of electrical components, control systems, retrofitting intelligent monitoring module, lower cost, can extend the life of the equipment, improve the stability of the operation, reduce the aging failure downtime, to adapt to the needs of high-traffic operations.

    IoT Real-time Monitoring

    Relying on IoT sensors, 24-hour remote monitoring of crane core component status, operation and environmental data, through the intelligent platform into operation and maintenance commands, in advance to lock the hidden dangers, formulate maintenance programs, to achieve proactive prevention and control; at the same time, linkage of the whole dock scheduling, reducing ineffective equipment operation and wear and tear.

    Automated Operation Reduces Errors

    Through automatic ship scheduling, berth intelligent allocation, precise positioning of containers, unmanned gantry crane operation and other automated means, reduce operator violations, fatigue operation errors, optimize operational consistency, avoid overloading of equipment, and reduce the risk of downtime from the source.

    Optimize Spare Parts and Maintenance Resources

    Yard planning is closely related to crane downtime, irrational stockpile layout will lead to frequent reversal of the crane, long-distance walking, significantly aggravating the wear and tear of equipment.

    With the help of digital twin technology, high-flow terminals can build a three-dimensional visualization model of the terminal to achieve precise positioning of containers, intelligent allocation of stacking positions, maximize the use of yard space, reduce repeated crane handling and idling operations, reduce equipment loss from the source of operation, and indirectly reduce the probability of downtime.

    Refinement of spare parts management, to eliminate the shortage of spare parts delayed maintenance. Untimely supply of spare parts is a key factor in prolonging crane downtime, especially wire rope, drums, bearings and other wear parts, as well as customized core components, once out of stock, the maintenance period will be significantly lengthened.

    High-flow terminals need to establish a refined spare parts inventory management system, combined with crane failure data, wearing parts loss cycle, reasonable reserves of core spare parts and high-frequency wearing parts, and give priority to ensure that the inventory of high-wear, high-value parts is sufficient; at the same time to establish a stable spare parts purchasing channels, for the customization of the components in advance, to avoid infinite prolongation of downtime due to the shortage of spare parts.

    Improve Workforce Efficiency and Operational Standards

    Licensed operators and regular training to enhance operational professionalism. High-traffic terminals must strictly implement the operator licensing system, all shore bridge, gantry crane operators must hold international or domestic recognized professional qualifications, familiar with the port crane safety practices and standard operating procedures.

    At the same time, abandon the concept of “a training for life”, regular retraining and practical assessment, for the special requirements of high-flow operating scenarios, to strengthen the standardized operation, emergency response, daily inspection and other skills training, synchronized with the Division of the rigging workers to collaborate on training, to open up the operation team and operation and maintenance team collaboration barriers, to reduce the failure to work together, Improve the inspection and monitoring system.

    Improve the inspection and monitoring system

    Normalized inspection is the last line of defense to prevent and control crane downtime, high-flow terminals need to abandon the “heavy maintenance, light inspection” of the wrong concept, the development of graded inspection plan, combined with equipment operation data rather than simply fixed calendar, to carry out daily inspection, special inspection and in-depth overhaul.

    Daily pre-shift inspection is completed by the operator, focusing on the investigation of safety hazards and intuitive failures; special inspection is completed by the operation and maintenance team, focusing on the core components of the operating state; in-depth inspection is carried out regularly, covering the steel structure, control system, hydraulic system and other full-dimensional components, so that hidden problems are discovered and disposed of as early as possible.

    The terminal can join hands with professional crane service providers to carry out O&M compliance checking and targeted rectification of loopholes in accordance with international standards and original factory specifications.

    At the same time, remote monitoring technology, relying on sensors to upload real-time equipment data, remote warning of hidden problems, operation and maintenance personnel can quickly dispose of minor problems; complex maintenance can be entrusted to a third-party professional organizations, double guarantee maintenance quality.

    FAQ

    Q1: What is the most effective way to reduce the downtime of high-flow quay cranes?

    Q2:How can automation technology reduce crane downtime?

    A2:Automation can significantly reduce the probability of human error, while optimizing the linkage scheduling of ships, berths and yards, reducing ineffective crane operations and overloading, improving operational coherence, and reducing downtime triggers from both operational and operational dimensions.

    Q3:Why is spare parts management vital to the normal operation of cranes?

    A3:High flow terminal operation is uninterrupted, once the core spare parts shortage, the maintenance period will be greatly extended, even small faults can cause long downtime, especially customized components, adequate spare parts inventory can make the maintenance work quickly to the ground, maximize the compression of downtime.

    Q4: How should the maintenance frequency of harbor cranes be determined?

    A4:It can not simply follow the fixed calendar cycle, need to combine the equipment operation data, frequency of operation, load intensity to develop a dynamic maintenance plan, and must implement the daily pre-shift safety inspection, strictly follow the original factory recommended maintenance cycle, high-flow operating scenarios need to be properly encrypted maintenance frequency.

    Q5: Can small and medium-sized high-traffic terminals implement these downtime reduction strategies?

    A5:Completely possible, all strategies are scalable, small and medium-sized terminals can start from the basic preventive maintenance, licensed operator training, spare parts management, and then gradually land IoT monitoring, predictive maintenance and other advanced technologies, step by step to achieve the goal of reducing downtime.

    Q6: What are the most avoidable causes of downtime for harbor cranes?

    A6: One is the unqualified operator’s illegal operation, and the other is the inefficiency of yard scheduling and operation planning, both of which do not require high technical investment, and can be completely avoided through standardized management, professional training and process optimization, which is the preferred breakthrough for downtime reduction.

    Henan Mine CraneDiscuss your requirements ↗
  • How To Reduce Long-Term Maintenance Costs Of Overhead Cranes

    How To Reduce Long-Term Maintenance Costs Of Overhead Cranes

    How To Reduce Long-Term Maintenance Costs Of Overhead Cranes

    In the field of industrial production, bridge cranes are the core equipment for workshop logistics and heavy material handling. Their operating stability directly affects production efficiency and enterprise operating costs.Most companies often pay attention to the initial investment when purchasing cranes, but ignore the control of long-term maintenance costs.According to industry statistics, the total maintenance cost of the crane during the 15-year service cycle can reach 25%-35% of the original value of the equipment, and the production losses caused by unplanned downtime are even more incalculable.This article will explain in detail the practical strategies to reduce the long-term maintenance costs of bridge cranes from the eight core dimensions of selection, operation and maintenance, and technology upgrade, so as to help enterprises achieve the optimal cost of the whole life cycle of equipment.

    Why Overhead Crane Maintenance Costs Matter

    Rising maintenance and downtime costs

    With the increase of the service life of the equipment, the wear and aging of the parts of the bridge crane will gradually become prominent, and the maintenance cost will increase year by year.On the one hand, frequent failure repairs require a lot of manpower, material and financial resources, especially the secondary maintenance rate of non-original parts is extremely high. Data show that the secondary failure rate of cranes using inferior parts is 2.3 times that of regular parts, which further pushes up maintenance expenditures.On the other hand, the shutdown and shutdown caused by the failure of the bridge crane will disrupt the production plan, causing indirect losses such as order delays and production capacity declines. For manufacturing companies with high daily operating intensity, the loss of a single-day shutdown can reach tens of thousands of yuan.

    Importance of reducing lifecycle costs

    Reducing the life cycle cost of Henan Mine Crane manufactured bridge cranes is a key measure for enterprises to enhance their core competitiveness.The whole life cycle cost not only includes the initial procurement cost, but also covers long-term maintenance, repair, upgrade, energy consumption and many other expenses.Through scientific cost control, the maintenance cost of bridge cranes can be reduced by more than 40%, while extending the service life of equipment, improving the utilization rate of equipment, and achieving the dual goals of cost reduction and efficiency.For enterprises, optimizing crane operation and maintenance costs is essentially a reasonable allocation of production resources, which can build a solid foundation for the long-term development of enterprises.

    Choose The Right Crane Design Initially

    Match cranes with working conditions

    Selection is the first step in controlling long-term maintenance costs. The core principle is to accurately match the bridge crane with the actual working conditions.Enterprises need to combine workshop span, lifting weight, operating frequency, ambient temperature, material characteristics and other factors to choose the appropriate crane type.For example, cranes made of high-temperature resistant materials need to be selected in high-temperature environments. In scenarios of frequent operations, priority should be given to durable models to avoid premature equipment wear and frequent failures due to improper selection, thereby increasing maintenance costs.

    Select durable crane components

    The durability of parts directly determines the maintenance frequency and cost of bridge cranes.In the selection of models, priority should be given to high-quality parts that have been verified by the market, such as wear-resistant wheels, high-strength wire ropes, and reliable electrical components.Although the initial investment in high-quality parts is slightly higher, it can significantly reduce the incidence of failures, reduce the frequency of replacement, and significantly save maintenance costs in the long run.For example, the selection of high-quality frequency conversion speed control system can reduce mechanical shocks and electrical failure rates, and the payback period usually does not exceed two years.

    Consider customized crane solutions

    For companies with special operating needs, customized Henan Mine Crane manufactured bridge crane solutions are an effective way to reduce long-term costs.The customized design can optimize the structure and performance of the equipment according to the unique working conditions of the enterprise, and avoid the functional redundancy or insufficient performance of the general-purpose crane.For example, for scenarios where workshop space is limited, compact bridge cranes are customized.According to the needs of high-precision handling, customized models with precise positioning function can not only improve operating efficiency, but also reduce maintenance problems caused by poor equipment adaptability.

    Establish A Preventive Maintenance Program

    Create regular inspection schedules

    Preventive maintenance is the core means to reduce long-term maintenance costs, and regular inspections are the basis for preventive maintenance.Enterprises need to establish a scientific inspection system, and formulate daily, weekly, monthly, and quarterly inspection plans based on the operating intensity and service life of the crane.The inspection content should cover the operating status of the equipment, the wear and tear of parts, the lubrication system, the electrical system, etc., so as to detect potential hidden faults in a timely manner and avoid small faults from turning into major problems.For example, the straightness and elevation of the track are measured once a month to confirm that the thermal expansion deformation does not exceed the allowable range to prevent abnormal track wear.

    Maintain critical crane components

    The key components of bridge cranes, such as wire ropes, brakes, bearings, motors, etc., are the key objects of maintenance.It is necessary to carry out regular maintenance of key parts in accordance with the requirements of the equipment manual, including cleaning, lubrication, fastening, adjustment, etc.For example, regularly check the wire rope for lubrication and wear, and replace the wire rope with excessive wear in time.Adjust the clearance of the brake to ensure stable braking performance and avoid downtime and increased maintenance costs caused by the failure of key components.

    Replace parts before failure

    Passive maintenance often leads to a significant increase in maintenance costs, and early replacement of parts that are about to fail can effectively avoid sudden failures.Through regular inspections and condition monitoring, grasp the wear law and service life of parts and components, and replace them in time before the parts reach the limit of service life.This kind of ”prevention before it happens” maintenance method can not only reduce the loss of sudden downtime, but also reduce the difficulty and cost of maintenance. Compared with passive maintenance, it can save more than 50% of the comprehensive cost.

    Improve Crane Operation And Management

    Train operators properly

    The professional level of operators directly affects the service life and maintenance costs of bridge cranes.Enterprises need to conduct systematic training for operators, including equipment operating procedures, safety precautions, daily inspection points, emergency handling of faults, etc.Qualified operators can standardize the operation of equipment to avoid equipment damage caused by improper operation. At the same time, they can detect abnormal conditions in the operation of the equipment in a timely manner, report and deal with them in a timely manner, and reduce the cost losses caused by the expansion of failures.

    Avoid common operating mistakes

    In actual operation, some common misoperation will accelerate equipment wear and increase maintenance costs.For example, overloading operations can cause deformation of the structure of the bridge crane and damage to parts.Emergency stop and emergency start will produce greater mechanical impact and damage the transmission components.Illegal operations can cause safety accidents and damage equipment at the same time.Therefore, it is necessary to standardize the behavior of operators, eliminate problems such as overload and illegal operations, develop good operating habits, and reduce equipment failures from the source.

    Perform daily equipment checks

    Daily inspection is an important part of timely detection of equipment abnormalities. Operators need to conduct basic inspections of bridge cranes before and after daily operations.The inspection content includes the appearance of the equipment, the status of the wire rope, the sensitivity of the brake, the limiting device, the lubrication condition, etc., and then start the operation after confirming that the equipment is not abnormal.There is no need to invest a lot of time in daily inspections, but it can effectively investigate potential hidden dangers and avoid major problems caused by small failures. Long-term persistence can significantly reduce maintenance costs.

    overhead crane maintenance costs

    Apply Smart Maintenance Technologies

    Use condition monitoring systems

    With the development of industrial intelligence, intelligent maintenance technology has provided a new path for Henan Mine Crane manufactured bridge cranes to reduce costs and increase efficiency.The condition monitoring system can collect crane operating data in real time through sensors, such as vibration, temperature, current, wear and other parameters, and monitor the operating status of the equipment in real time.When the equipment is abnormal, the system will issue an early warning in a timely manner to help maintenance personnel quickly locate the point of failure, reduce troubleshooting time and improve maintenance efficiency.Data show that unplanned downtime of cranes deploying remote operation and maintenance systems can be reduced by 30%-45%.

    Adopt predictive maintenance methods

    Predictive maintenance is based on equipment operation data and AI analysis to predict the service life of parts and the probability of failure, so as to formulate an accurate maintenance plan.Compared with traditional preventive maintenance, predictive maintenance is more targeted, which can avoid the problem of excessive maintenance or insufficient maintenance, and further reduce maintenance costs.For example, by analyzing the operating current and temperature data of the motor, predict the risk of failure of the motor, and carry out maintenance or replacement in advance to avoid the high maintenance costs caused by the motor burning down.

    Improve maintenance efficiency

    The application of intelligent maintenance technology can greatly improve maintenance efficiency and reduce labor costs.For example, the remote operation and maintenance system can realize the remote monitoring and fault diagnosis of bridge cranes, and maintenance personnel can investigate some faults without going to the site.The intelligent maintenance management platform can automatically generate maintenance plans, record maintenance data, manage spare parts inventory, optimize the maintenance process, reduce the cumbersome manual operation, and make maintenance work more efficient and accurate.

    Optimize Lubrication And Parts Management

    Follow proper lubrication practices

    Lubrication is an important part of the maintenance of bridge cranes. Reasonable lubrication can reduce the wear and tear of parts, extend the service life of equipment, and reduce maintenance costs.According to the requirements of the equipment manual, enterprises need to choose suitable lubricants, such as NLGI-2 grade lithium-based grease, with temperature resistance of -20℃ to 130℃, strong adhesion, and lubricate bearings, hinge seats, wire ropes and other components in accordance with the specified lubrication cycle and lubrication amount.At the same time, the status of the lubrication system needs to be checked regularly to avoid problems caused by insufficient or excessive lubrication.

    Manage spare parts effectively

    The rationality of spare parts management directly affects maintenance efficiency and cost.Enterprises need to establish a sound spare parts inventory management system, according to the model, service life and maintenance needs of bridge cranes, reasonably reserve commonly used spare parts, such as wire ropes, brake linings, bearings, etc., to avoid maintenance delays caused by the shortage of spare parts, while avoiding the waste of funds caused by the backlog of spare parts.In addition, priority should be given to the selection of spare parts from the original factory or formal channels to ensure the quality of spare parts and reduce the probability of secondary maintenance.

    Prevent corrosion damage

    For bridge cranes operating in humid and corrosive environments, corrosion is an important factor that leads to equipment damage and increased maintenance costs.Enterprises need to take effective anti-corrosion measures, such as regular rust removal and painting of the metal structure of the crane, and the selection of parts made of corrosion-resistant materials to avoid the erosion of the equipment by rain and corrosive gases.At the same time, it is necessary to keep the operating environment of the equipment dry and clean, reduce the impact of corrosive media on the equipment, and extend the service life of the equipment.

    Extend Crane Life With System Upgrades

    Upgrade outdated control systems

    With the continuous progress of technology, old control systems often have problems such as low operating efficiency, high failure rate, and high energy consumption.Upgrading the old control system, such as replacing it with an intelligent frequency conversion control system, can improve the operating accuracy and stability of the equipment, reduce the electrical failure rate, and reduce energy consumption.Data show that the average annual electricity bill expenditure of intelligent models can be reduced by about 27% compared with traditional models, which can significantly save operating costs in the long run.

    Replace aging components

    For bridge cranes with a long service life, some parts will have problems such as aging and severe wear, and it is difficult to restore their performance even if they are frequently maintained.At this time, key aging parts, such as motors, reducers, wheel sets, etc., need to be replaced in time to avoid frequent failures and increased maintenance costs caused by aging parts.Although there is a certain initial investment in replacing aging parts, it can significantly improve the performance of the equipment and extend the service life of the equipment. In the long run, it has a high price/performance ratio.

    Improve energy efficiency

    Optimizing the energy consumption performance of Henan Mine Crane manufactured cranes is also an important way to reduce long-term operating costs.In addition to upgrading the control system, the energy consumption of the equipment can also be reduced by replacing energy-saving motors, optimizing the operating parameters of the equipment, and adopting regenerative braking technology.For example, regenerative braking technology can recover the energy generated during the descent of the crane and reduce energy waste. The payback period is usually 3-5 years, and the long-term energy-saving benefits are significant.

    Henan Mine Crane Factory Custom

    Reducing the long-term maintenance cost of bridge cranes is not an overnight task, but requires the establishment of a long-term and systematic maintenance plan.Enterprises need to combine their own production needs and equipment conditions, starting from multiple dimensions such as selection, operation and maintenance, technology upgrading, and spare parts management, formulate a scientific maintenance strategy, transform passive maintenance into active prevention, and realize cost control throughout the life cycle of equipment.

    In the long run, investing in reliable Henan Mine Crane Factory crane solutions is the core guarantee for reducing maintenance costs.Whether it is high-quality equipment in the selection stage, intelligent technology application and professional service support in the operation and maintenance stage, enterprises need to make reasonable investment.Through scientific cost control and reasonable resource investment, it can not only reduce the long-term maintenance cost of the crane, but also improve the operating efficiency and stability of the equipment, provide strong support for the production and development of the enterprise, and achieve the long-term goal of cost reduction and efficiency.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Reduce Energy Consumption in Port Crane Operations?

    How to Reduce Energy Consumption in Port Crane Operations?

    How to Reduce Energy Consumption in Port Crane Operations?

    At present, domestic ports are promoting low-carbon transformation and reducing operating costs. As the main terminal operating equipment, port cranes account for more than 60% of the total energy consumption of port operations.Traditional cranes have high energy consumption and unstable energy efficiency, which not only drives up electricity consumption and operation and maintenance expenses, but also does not meet the requirements of green port construction.For port operations, equipment management and other related enterprises, this article combs out a set of practical plans for energy saving and consumption reduction of cranes with strong landing properties.

    What Causes High Energy Consumption in Port Cranes?

    The problem of high energy consumption of port cranes is not caused by a single factor, but the result of multiple factors such as equipment operation mechanism, operating conditions, and standby energy consumption.For mainstream cranes such as port shore bridges, rail cranes, and tire cranes, the operation process includes multiple links such as lifting, walking, standby, and auxiliary operation. The unreasonable operation of each link will cause energy loss. Among them, dynamic operation energy consumption and long-term standby energy consumption are the two core sources of waste.The following is a breakdown of the core operation scenarios, and an in-depth dismantling of the core incentives for high energy consumption.

    Hoisting and lowering

    Lifting and descending are the most energy-consuming operations of port cranes, accounting for about half of the energy consumption of the whole machine.The load adaptability of traditional old motors is poor, frequent start-stop and variable speed are prone to invalid power consumption, and the energy utilization rate during light-load operations is less than 70%.More seriously, the equipment descent process relies on resistance braking, and all the gravity potential energy of the cargo is converted into heat energy and lost in vain. Not only is energy wasted, but it will also cause equipment to heat up and aging lines, coupled with unstable manual operation speed and frequent start and stop, which further exacerbates the waste of energy consumption and equipment loss.

    Trolley and gantry travel

    Trolley and gantry walking belong to high-frequency operations. Although the single energy consumption is low, the cumulative energy consumption accounts for 25%-30% of the whole machine, which is the main reason for the waste of hidden energy consumption in the terminal.The traditional transmission structure is highly rigid, and frequent start-stop and speed regulation of equipment will produce a lot of inertial energy consumption.Manual operation often has problems such as blind speed-up, emergency braking, and path redundancy. Repeated displacement and invalid walking are common. Old equipment lacks the ability to adjust speed accurately, which not only consumes additional power, but also exacerbates mechanical wear and tear, and the overall energy consumption and waste will be further magnified under large-scale operations.

    Auxiliary and standby power

    The energy consumption of auxiliary equipment operation and standby is the most neglected energy consumption vulnerability of port cranes, and the average daily energy consumption of the whole machine is 15%-20%.Port cranes are on standby for 24 hours a day, and long-term no-load power is turned on during operation gaps, ship waiting, and shift handover, and standby power consumption remains high.At the same time, auxiliary equipment such as lighting, hydraulics, cooling, etc. continue to operate around the clock, without intelligent start-stop control function, coupled with aging of old equipment lines, leakage, voltage instability and other problems, long-term continuous invalid energy consumption, accumulating over time, resulting in a lot of energy waste.

    How Can Electrification Improve Port Crane Energy Efficiency?

    Electrification transformation is the basic core plan for energy saving and consumption reduction of port cranes, as well as the core path for upgrading traditional fuel-fired cranes and improving the quality of old electric equipment.Compared with the traditional power model, the electrification system thoroughly optimizes the energy consumption structure from the three dimensions of power source, drive system, and energy recovery, significantly reduces invalid energy consumption, improves energy utilization, and reduces exhaust emissions and operating noise. Perfectly adapted to green port construction standards.Combined with industry landing cases, electrification transformation can reduce the comprehensive energy consumption of cranes by 25%-40%, with significant energy-saving effects and strong stability.

    Electric vs. diesel power

    The core difference between diesel power and electric power directly determines the basic energy consumption level and operating cost of Henan Mine Crane Factory supply port crane.Traditional diesel-driven tire cranes and mobile cranes have extremely low energy utilization rates. Only about 30% of diesel combustion energy can be converted into effective operating power. The rest is wasted in the form of heat, exhaust gas, and noise. At the same time, insufficient fuel combustion, idle speed, fuel consumption, variable speed loss and other problems are prominent, not only high energy consumption, but also a large number of exhaust gas pollutants will be generated, and operation and maintenance costs remain high.

    The pure electric drive mode completely solves the core disadvantages of fuel power, the power energy conversion efficiency can reach more than 85%, the energy transmission loss is extremely low, there is no combustion waste, and no idle redundancy loss.At present, the mainstream equipment electrification transformation plan in the industry retains the emergency function of the diesel engine set, adopts MAINS power supply for conventional operations, and flexibly switches between special operating conditions in transition, taking into account energy saving and practicality.The measured data show that under the same operating volume, compared with diesel cranes, electric cranes reduce the average annual energy consumption cost of a single equipment by 40%-60%, while significantly reducing exhaust emissions, which meets the requirements of port environmental protection compliance.

    Energy-efficient motors and VFDs

    High-efficiency and energy-saving motors and frequency conversion speed control systems (VFDs) are the core hardware support for electrification and energy saving, and they are also the most cost-effective solution for the energy-saving transformation of old cranes.Ordinary asynchronous motors equipped with traditional cranes have low energy efficiency levels, and their operating efficiency declines significantly under light-load and no-load conditions. Long-term operation energy consumption is serious, and they cannot adapt to dynamic load changes. Speed regulation relies on mechanical braking, and energy consumption is greatly wasted.

    Regenerative braking and energy recovery

    Regenerative braking and energy recovery technology are the core highlights of electrification and energy saving, which can realize energy recycling and completely solve the problem of energy waste in the descent and braking links.The traditional crane braking mode is energy consumption braking, which converts all kinetic energy and gravity potential energy into heat energy loss, which is the core pain point of the waste of energy consumption of the whole machine.The regenerative braking system is equipped with a two-way converter, which can convert excess gravity potential energy and kinetic energy into standard alternating current under working conditions such as cargo descent, equipment braking, and trolley return, and feed it back to the power grid or store it in the energy storage unit.

    At present, the mainstream energy recovery system in the industry can achieve a power recovery and utilization rate of 25%-40%. Some Henan Mine Crane Factory supply new port cranes equipped with supercapacitor energy storage equipment can store the recovered power for high-power conditions such as equipment start-up and acceleration to further reduce the peak energy consumption load of the power grid.This technology is perfectly adapted to the operating characteristics of high-frequency lifting and frequent braking of port cranes. It is the core technology for cost reduction and efficiency enhancement of large-scale ports. It has been widely deployed in large terminals such as Shanghai Port and Qingdao Port, and the measured comprehensive energy-saving effect can reach more than 20%.

    port crane energy consumption

    How Can Port Crane Operations Be Optimized to Save Energy?

    The upgrading of hardware electrification is the basis for energy saving, and the refined optimization of operating processes is the key to low-cost and continuous improvement of energy-saving effects.A large number of actual port data show that under the same equipment conditions, standardized and intelligent operation control can achieve 15%-25% additional energy-saving benefits.There is no need for large-scale equipment transformation. Only by optimizing the operation action, controlling the standby time, and upgrading the scheduling mode, the energy-saving effect can be quickly implemented, and it can be adapted to the lightweight energy-saving transformation needs of various ports, large, medium and small.

    Optimize crane movements

    Irregular crane operation actions, redundant operating paths, and unreasonable speed control are the most important human-made energy consumption wastes in manual operation mode.In traditional manual operations, in order to pursue operational efficiency, operators generally have irregular operations such as rapid acceleration, rapid braking, ultra-high-speed operation, and repeated displacement. Each invalid action will produce additional energy consumption and mechanical loss.

    The core of action optimization is to establish a standardized operating process, implement operating guidelines for uniform speed operation, smooth start and stop, and plan the optimal walking operating path.According to the cargo tonnage, operating height, and yard location, exclusive operating parameters are formulated to prevent blind speed-up and emergency braking.Unify the walking routes of trolleys and gantry frames to avoid invalid operations such as redundant walking across regions and repeated alignment.At the same time, standardize the rhythm of lifting operations, smooth lifting of heavy loads and low speeds, and uniform speed operation of light loads to reduce the impact of energy consumption caused by switching working conditions.Through standardized action control, the energy consumption of a single operation can be effectively reduced, mechanical wear and tear can be reduced, and the two-way benefits of energy saving and equipment longevity can be realized.

    Reduce idle time

    Invalid standby time is too long, which is an important reason for the waste of normalized energy consumption of port cranes. Most terminal cranes have an average standby time of more than 8 hours a day, and the cumulative loss of standby energy consumption is great.In scenarios such as operation gaps, ship waiting, cargo transfer and connection gaps, and personnel shifts, the equipment is powered on at no load for a long time, and the auxiliary equipment continues to operate, resulting in a lot of invalid energy consumption.

    Targeted optimization can be implemented in both directions from system control and equipment transformation. At the system level, equipment start-stop control specifications are formulated, and the main drive system and idle auxiliary equipment are turned off in time when there is no operating task, so as to eliminate long-term no-load standby.At the equipment level, an intelligent standby control module is installed to realize low-load sleep of the equipment, timed power failure, induction start and stop under working conditions, and automatic switching of energy-saving modes between operations to reduce standby power consumption.At the same time, optimize the operation convergence process, compress the waiting time for ship berthing, cargo distribution, and team handover, maximize the effective operation time of equipment, reduce invalid standby energy consumption, and reduce the average daily energy consumption by 10%-18% after landing.

    Optimize crane scheduling

    Unreasonable scheduling of port crane clusters can lead to uneven equipment workload, repetitive operations, and no-load rushes. It is the core cause of the high overall energy consumption of large-scale terminals.The traditional manual scheduling model lacks overall coordination, and it is prone to problems such as multiple equipment in a single area, no-load standby of equipment in remote areas, and unbalanced distribution of light and heavy operations, resulting in a large amount of cluster energy consumption and waste.

    The core of optimized scheduling is to realize global intelligent overall scheduling, combining ship arrival time, cargo throughput, yard distribution, and equipment working conditions to scientifically allocate crane operation tasks.Avoid the situation where a single equipment is overloaded with high-frequency operations and multiple equipment are on standby invalid, balance the operating load of the equipment, and reduce long-distance shift operations across regions.At the same time, reasonably plan the operating shifts, take advantage of the low electricity prices of the power grid at peak times, optimize the high-power operating hours, and reduce the peak electricity costs.The scientific scheduling scheme can reduce the energy consumption of the overall crane cluster in the port by about 15%, and greatly improve the overall energy efficiency of the terminal operation.

    How Does Automation Reduce Port Crane Energy Consumption?

    Automation and intelligence are high-end solutions for energy saving and consumption reduction of Henan Mine Crane Factory supply port cranes, which completely solve the problems of randomness, irregularity and inefficiency of manual operation.Relying on intelligent sensing, algorithm control, and automatic positioning technology, it realizes precise control and intelligent optimization of the whole process of crane operation, avoids the waste of energy consumption caused by human operation from the root cause, and adapts to high-intensity and high-frequency port operation scenarios to achieve energy-saving, high-efficiency, and stable trinity upgrades. It is the core standard of smart port construction.

    Automated movement and positioning

    Manual alignment is prone to deviation, repeated displacement and emergency start and stop, resulting in a lot of invalid energy consumption and time loss.The automated precise positioning system can plan the optimal walking path according to on-site working conditions, realize automatic driving, smooth speed regulation and precise alignment, avoid redundant actions throughout the process, and greatly reduce the inertial energy consumption caused by start and stop.The parameters of the entire operation process are stable and controllable, so as to get rid of the arbitrariness of manual operation.Combined with the actual application data of Qingdao Port, the no-load return energy consumption of the shore bridge equipped with automatic positioning function can be reduced by 22%, and the overall operating energy efficiency can be significantly improved.

    Anti-sway and intelligent control

    Crane start-stop and variable-speed operations can easily cause the cargo to sway. Manual operation requires waiting for the cargo to stabilize and repeatedly correcting the position, which not only slows down the pace of the operation, but also continues to produce excess energy consumption.The intelligent anti-swing control system can monitor the swing state in real time, dynamically fine-tune the operating parameters of the motor through algorithms, and actively suppress the shaking of the goods without manually waiting for correction.This technology effectively shortens the operating cycle and reduces the invalid operating loss of equipment. In high-frequency container loading and unloading scenarios, it can stably reduce the operating energy consumption by 12%-15%, taking into account energy saving and operating safety.

    Energy-efficient operating strategies

    Traditional manual operation only relies on experience to regulate equipment, and cannot dynamically adapt energy consumption according to real-time loads and working conditions, which is likely to cause energy waste.Relying on big data and AI algorithms, the automated intelligent system monitors parameters such as lifting height, load, and operating distance in real time, and automatically matches the optimal energy-saving operation strategy.The equipment can intelligently distinguish between heavy-duty, light-load and no-load operating conditions, flexibly adjust the operating speed and start-stop logic, reduce the output of high-energy-consuming operating conditions, and optimize the operation rhythm of multiple equipment clusters, balance the load and peak-off operations, and comprehensively tap the overall energy-saving space of the terminal.

    What Is the Most Effective Way to Reduce Port Crane Energy Consumption?

    Combining the three categories of energy-saving solutions mentioned above: hardware upgrade, process optimization, and intelligent empowerment, a single energy-saving method has certain limitations. The cost of simple equipment upgrade is high, and the upper limit of energy-saving for simple process optimization is low. It is difficult to implement a single automation transformation.Combining the landing cases and measured data of major ports around the world, the comprehensive solution that integrates electrification hardware upgrade, refined operation optimization and intelligent automation empowerment is currently the most efficient, stable and cost-effective crane energy-saving and consumption-reducing method, which can achieve a comprehensive energy consumption reduction of 35%-50%, and is suitable for various operating scenarios of old and new terminals.

    Upgrade drive and recovery systems

    The upgrade of the drive and energy recovery system is the core hardware foundation for energy saving and consumption reduction, and it is a prerequisite for achieving significant energy saving.Inefficient motors of old equipment, traditional braking systems, and drive structures without frequency conversion control are the root causes of high energy consumption.Priority is given to completing the core hardware upgrade, replacing the first-class energy-efficient and energy-saving motor, equipped with a VFD frequency conversion speed control system, and supporting a regenerative braking energy recovery device to solve the problem of basic energy consumption and waste from the source of power.

    The program has the most direct energy-saving effect and the strongest stability. It can solve the core energy consumption pain points of lifting, braking, and walking at once, and the basic energy-saving benefits can reach 25%-40%.For ports with limited budgets, priority can be given to frequency conversion transformation and energy recovery system installation, so as to quickly obtain significant energy-saving effects at the lowest hardware transformation cost. It is the hardware upgrade method with the highest neutral price ratio of all energy-saving solutions.

    Optimize operating practices

    Normalized operation optimization is the key to low-cost and continuous amplification of energy-saving effects, and it is a long-term energy-saving method with zero cost and high return.After the hardware upgrade, it is equipped with standardized operating specifications, a refined scheduling system, and a strict standby control mechanism, which can further tap the potential of energy saving, make up for the shortcomings of hardware energy saving, and solve the waste of energy consumption caused by human operation and management loopholes.

    Through standardized personnel training, operation process control, intelligent scheduling landing, and standby energy consumption control, an additional energy-saving benefit of about 15% can be achieved on the basis of hardware energy saving.At the same time, a standardized operating model can reduce equipment failures and losses, reduce long-term operation and maintenance costs, extend the service life of equipment, and realize the long-term value of energy saving, cost reduction, quality improvement, and efficiency enhancement. It is a basic control method that all ports must implement.

    Combine electrification and automation

    The deep integration of electrification and automation is the best and ultimate solution for energy saving and consumption reduction of Henan Mine Crane Factory supply port cranes, and it is also the development trend of smart green ports.Electrification solves the problems of high energy consumption of equipment and hardware and energy that cannot be recovered, and automation solves the problems of irregular manual operation, inefficient operation, and unreasonable scheduling. The two complement each other and enable them to completely open up the energy-saving link of the whole crane process.

    Electrification hardware provides a stable foundation for intelligent automation control, and automation algorithms can maximize the energy-saving advantages of electrified equipment and realize optimal dynamic energy consumption control.The landing cases of leading ports at home and abroad have proved that after the integration and transformation of the dual-system, the comprehensive energy consumption of port cranes can be reduced by 40%-50%, the operating efficiency can be increased by more than 30%, and the equipment failure rate has been significantly reduced. At the same time, it fully meets the requirements of the dual-carbon policy and environmental protection assessment, and helps the port achieve low-cost, green, and intelligent long-term development.

    Henan Mine Crane Factory Custom Custom

    The energy saving and consumption reduction of port cranes is not a single equipment transformation, but a systematic project covering hardware systems, operating processes, intelligent control, and operation management.Investigate the pain points of energy consumption and waste in lifting, walking, and standby from the root cause, rely on electrification transformation to consolidate the foundation of energy saving, tap the potential of lightweight energy saving through operation optimization, and realize intelligent and accurate energy saving with the help of automation technology, and finally maximize the energy-saving effect through a combination of electrification, automation and refined operations.

    For port companies of different sizes and equipment working conditions, Henan Mine Crane Factory can provide customized and phased crane energy-saving transformation solutions, which are accurately adapted to various budgets and operating scenarios.Priority can be given to frequency conversion upgrades and energy recovery and lightweight transformation of old equipment, which can be quickly implemented and quickly returned to cost.Small and medium-sized terminals can achieve zero cost, efficiency and quality improvement through process optimization.Large-scale smart ports can implement integrated electrification and automation transformation plans.Relying on mature equipment technology and landing experience, it will help major ports easily achieve cost reduction and efficiency enhancement and green and low-carbon transformation, and firmly occupy the core advantages of low-carbon development in the industry.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Reduce Container Handling Costs in Modern Ports?

    How to Reduce Container Handling Costs in Modern Ports?

    How to Reduce Container Handling Costs in Modern Ports?

    In recent years, the operating pressure of global container terminals has continued to rise, labor costs have risen, fuel prices have fluctuated, container arrivals have steadily increased, stricter environmental emission requirements and shorter ship turnover requirements have been superimposed, and the reduction of container handling costs directly determines the market competitiveness and actual profitability of terminals.
    When many terminals mention cost reduction, the first reaction is to lower the purchase price of equipment.However, from the perspective of long-term operation, the purchase price difference of a single equipment is far less than the long-term expenses caused by unreasonable selection, inefficient scheduling, high energy consumption and high downtime.As a professional port lifting equipment manufacturer, Henan Mine Crane has served port projects of different scales around the world. The real cost adjustment is the entire chain improvement covering yard planning, equipment selection, energy structure, and maintenance system.This content collates practical operation strategies that can be implemented to help operators reduce long-term operating expenses on the premise of ensuring operational capability.


    Cost components of container handling

    Many operating costs are only procurement and fuel, in fact, the complete cost includes three categories.
    The first category is equipment investment cost, namely CAPEX, covering the procurement, installation and commissioning of STS quayside crane, RTG tire gantry crane, RMG rail gantry crane, container straddle carrier, dock tractor and other equipment, as well as supporting infrastructure investment.
    The second category is operating costs, that is, OPEX, the highest proportion of energy costs, diesel, electricity, charging costs are included; followed by labor costs, drivers, maintenance personnel compensation expenses; there are maintenance spare parts, tire wear and tear such daily expenses, tire wear and tear for RTG, straddle transport such tire equipment, is a fixed expenditure that can not be ignored.
    The third category is hidden costs that are easy to ignore, such as truck waiting time, ship delay fines, idle equipment, efficiency losses caused by yard congestion, and downtime losses caused by sudden failures, which are often higher than book expenses.

    Optimize yard layout

    Unreasonable yard planning will make the equipment travel distance longer, fuel consumption increased, but also cause a large number of dumping operations, increase the workload of equipment for nothing.
    When planning the container area, it is necessary to divide the area according to the flow direction of the container, arrange the inlet container and the outlet container separately, set up the exclusive operation area for the refrigerator and dangerous goods container, store the empty containers in a centralized way, and minimize the trans-regional long-distance transfer.The cold chain container port area and dangerous goods container yard shall be divided into separate operation scope to reduce the extra distance caused by cross-transfer.
    The core is to reduce repeated dumping of boxes. Many storage yards have to empty two or three stacked boxes for one box due to chaotic planning, which consumes both energy consumption and time.Reasonable stacking planning can greatly reduce ineffective removal, reduce equipment operating load, and naturally reduce the cost of single box operation.This is also the core value of port yard layout optimization.

    Opt-in equipment configuration

    Different handling equipment adapts to completely different scenarios, and selecting the wrong model will directly increase long-term operating costs.The equipment selection of container terminal is the basis of cost reduction.
    RTG tire gantry crane is the main equipment of many storage yards, and the cost reduction space is also the largest.Existing diesel equipment can be modified by electric RTG, or electric RTG crane can be purchased directly, with hybrid system, remote control and automatic alignment function, which can not only reduce energy consumption, but also improve operation efficiency.
    RMG rail gantry crane is suitable for large-scale fixed storage yard, with higher stacking density, lower labor demand, low electrification operation cost and great automation upgrade potential. It is a common choice for large-scale hub ports and railway intermodal container stations. The long-term cost advantage after RMG automation upgrade is more obvious.
    Container straddle carriers are more flexible and suitable for storage yards with fast turnover and frequent adjustment of container areas. Small and medium-sized container terminals and inland dry port storage yards can be preferred.Through fleet optimization, replacement of electric models and adjustment of driving routes, straddle efficiency can also be improved and costs reduced.
    The efficiency of STS quayside crane directly affects the ship’s time in port. Upgrade crane anti-swing technology, crane automatic alignment and remote control functions, which can shorten the operation cycle of single ship, reduce ship delay loss and improve berth utilization rate.

    Common Container Handling Equipment Comparison

    Equipment Type Initial Investment Energy Cost Labor Demand Stacking Height Flexibility Best Application
    Diesel RTG Medium High Medium 4-6 layers Medium Medium-sized conventional yards
    Electric RTG Medium-high Low Medium 4-6 layers Medium Yards with stable power supply
    RMG Crane High Very low Low 5-7 layers Very low Large fixed yards & rail terminals
    Straddle Carrier Medium Medium Low 2-4 layers Very high High-turnover flexible yards

    Advancing Electrification Transformation

    The volatility of diesel prices, coupled with tighter carbon emission controls in various regions, has led to higher operating costs for diesel equipment and risks of emission compliance.Electrification is the most direct way to reduce terminal energy consumption cost.
    The most mature scheme is to change diesel RTG into electric one. After the transformation, the energy consumption cost of single box is obviously reduced, and the equipment maintenance items are also less.For storage yards without fixed power supply conditions, hybrid port equipment can be used for transition first to gradually reduce fuel consumption.
    Lithium battery container straddle carriers and dock tractors are also very mature, suitable for short-distance high-frequency transfer scenarios.When calculating energy-saving benefits, it is necessary to combine the annual operation time, fuel consumption, local electricity price, and then calculate the battery life cycle to obtain a clear return cycle.
    This is also the core component of the green port equipment scheme. In many areas, there are policy subsidies for low-carbon ports, which can further dilute investment.

    Increase equipment utilization

    When equipment is idle, depreciation and fixed costs are always incurred, and the cost of single box operation is naturally high.To improve the utilization rate of port equipment, we can undertake more operations without adding new equipment.
    Equipped with container equipment fleet management system, real-time scheduling and operation dispatch, reduce equipment idle driving and waiting time.If conditions permit, AI yard scheduling system can be used to dynamically allocate equipment according to workload to avoid uneven busy and idle.
    Daily attention shall be paid to key operation indicators, such as hourly operation volume of single machine, equipment availability rate, empty driving ratio, energy consumption of single box, downtime, and improvement space shall be found with data to gradually improve overall operation efficiency.
    Automation and intelligent maintenance reduce labor and downtime costs
    The initial investment of automatic container terminal scheme is not low, but in the long run, it can greatly reduce manpower dependence, reduce equipment damage and cargo damage caused by human operation error, and have stronger operation stability.Instead of one step in place, we can start with remote port control transformation and automatic stacking, and gradually upgrade to realize port automation cost reduction.
    The maintenance end has changed from “repair after failure” to predictive maintenance of port equipment, monitoring motor temperature, vibration, braking state and hydraulic pressure through sensors, detecting fault signs in advance, and arranging scheduled maintenance.
    This can not only reduce the production loss caused by sudden shutdown, but also prolong the service life of equipment, and the cost control effect of port equipment maintenance is obvious.Equipped with equipment remote monitoring system, overseas projects can also quickly troubleshoot, reducing the time and cost of field service.

    Common Mistakes in Cost Reduction

    Many docks are easy to take detours.The most common is to focus only on the purchase price, low-cost equipment often high energy consumption, more failures, short life, full-cycle costs are higher.
    Some terminals are blindly automated, but they do not sort out the operation flow first. The problems of the flow itself are not solved, and the automation cannot play an effective role.
    There are also many projects that ignore long-term electrification planning and purchase all diesel equipment. In a few years, emission restrictions will be encountered, and the transformation will cost a sum of money.
    A total cost of ownership analysis of port equipment, including all expenditures over 10 to 15 years, can truly judge the economics of the proposal.Our port TCO analysis service can also help customers calculate long-term income accounts.

    FAQ

    How can ports effectively reduce container handling costs?

    It can be promoted from several dimensions: yard layout adjustment, equipment electrification transformation, automation upgrading, predictive maintenance and scheduling improvement. It can not be realized by one item alone, but system adjustment should be made in combination with its own working conditions.

    Are automated terminals cheaper to operate?

    The initial investment is higher, but in the long run, the labor cost is lower and the operation efficiency is more stable. The cost advantage of the whole life cycle will gradually appear. The specific return cycle depends on the operation volume and labor cost level of the terminal.

    Are electric RTGs cheaper than diesel RTGs?

    The purchase price is slightly higher, but the energy consumption and maintenance cost are lower, and the terminal with sufficient operation time can usually recover the price difference in a few years, so it is more cost-effective to operate for a long time.

    epilogue

    Reducing container handling costs is never by buying the cheapest equipment, but by adjusting the whole chain from yard planning, equipment selection to operation maintenance.
    Future container terminals will develop in the direction of smarter, lower energy consumption and less manual intervention. Only by laying out reasonable equipment schemes and operation systems in advance can we maintain cost advantages in long-term competition.

    Customized terminal cost optimization scheme

    Henan Mine Crane professional port crane equipment supplier, we can provide you with container terminal cost optimization assessment.You only need to provide annual throughput, existing equipment, yard layout, energy cost and automation goals, and our engineering team will issue targeted improvement solutions, covering RTG/RMG upgrade, straddle carrier selection, electrification route planning, smart port solutions and more.
    You can also contact us for free to receive the “Modern Port Container Handling Cost Reduction Self-Inspection List” to help you quickly sort out the improvement space of existing operations.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Reduce Container Handling Costs in Modern Ports? Complete Guide

    How to Reduce Container Handling Costs in Modern Ports? Complete Guide

    How to Reduce Container Handling Costs in Modern Ports? Complete Guide

    What can modern ports do to cut costs on container handling?

    In recent years, global container terminals have been under more and more pressure. Rising labour costs, fuel prices that keep going up and down, record-high container volumes, plus stricter environmental rules and shorter times for vessels to get ready to use again—all these things mean that cutting container handling costs will have a direct effect on how competitive a terminal is in the market and how much profit it makes.
    When it comes to saving money and getting more out of their kit, most terminals think the best thing to do is to bring down the price of equipment. But when you look at the long-term costs, the price difference for one piece of kit is nothing compared to the long-term costs of choosing the wrong equipment, poor scheduling, using too much energy, and times when the equipment is not working.
    Henan Mine Crane is a professional manufacturer of port crane equipment, and we’ve been involved in port projects of all sizes all over the world. To really get the most out of your costs, you’ve got to make improvements at every stage, from planning the yard to choosing the equipment, the energy structure, and maintenance systems. This article looks at some practical ways to cut long-term costs and keep things running smoothly.

    So, when it comes to working out how much it costs to handle containers, here’s the lowdown.

    The first category is capital expenditure (CAPEX), which includes ship-to-shore gantry cranes (STS), rubber-tired gantry cranes (RTG), rail-mounted gantry cranes (RMG), container stackers, and terminal tractors, as well as any related infrastructure investments.
    The second category is operating costs (OPEX). The biggest chunk of this is energy costs, like diesel, electricity, and charging fees. Then there’s labour costs, like wages for drivers and maintenance staff. And then there’s the day-to-day stuff like maintenance, spare parts and tyre wear costs. When it comes to wheeled equipment like RTGs and container handlers, tyre wear is a big fixed cost that can’t be ignored.
    The third category is all about hidden costs that people often don’t think about, like demurrage fees for waiting container trucks, penalties for vessel delays, efficiency losses due to equipment idling or yard congestion, and downtime losses caused by unexpected breakdowns. These hidden costs often end up being more than what’s shown on the books.

    If you make the most of the yard layout, you can cut down on waste right at the source.

    If the yard’s not planned properly, you’ll have to travel further with the equipment, use more fuel and do more container transfers, which all adds to the workload.
    When you’re planning container zones, it’s a good idea to divide the area based on how the containers are moving around. Import and export containers should be stored separately; we should have dedicated areas for refrigerated and hazardous materials containers; and empty containers should be consolidated to minimise long-distance transfers between zones. It’d be great if cold-chain container terminals and dangerous goods container yards could clearly mark out their operational areas. This would mean less extra travel distance for cross-zone transfer operations.
    The most important thing is to minimise container repositioning. In a lot of yards, because of poor planning, getting one container out often means moving two or three stacked containers – which is not only a lot of work, but also takes forever. If you plan your yard layout well, you can cut down on unnecessary movements, reduce the load on your equipment, and, of course, lower the handling cost per container. This is the main idea behind optimising port yard layout.

    Selecting the Right Equipment for the Yard

    Different handling equipment is suited for different scenarios. If you pick the wrong model, you’ll end up paying more in the long run. Picking the right kit for a container terminal is key to saving money.
    Rubber-Tired Gantry (RTG) Cranes are the main equipment in many yards and offer the best potential for cost reduction. You can retrofit existing diesel-powered equipment to electric RTGs or buy electric RTGs straight up. When you add hybrid systems, remote control, and automatic positioning, they can both cut energy consumption and improve how things are done.
    Rail-mounted gantry cranes (RMGs) are perfect for large, fixed yards. They offer higher stacking density, lower labour requirements, lower electrification operating costs, and significant potential for automation upgrades. They’re a popular choice for large hub ports and intermodal container terminals, and they’re even more cost-effective in the long run after automation upgrades are finished.
    These vehicles are perfect for places where containers are constantly moving around, as well as for small and medium-sized container terminals and inland dry ports. You can also make transfer vehicles more efficient and cut their costs by optimising your fleet, switching to electric models, and adjusting driving routes.
    STS gantry cranes are key to how long a vessel spends in port. If you upgrade to anti-sway technology, automatic crane positioning and remote control, you can shorten the loading and unloading cycle for each vessel, reduce demurrage charges and improve berth utilisation.

    Here’s a quick rundown of some of the most common container handling equipment.

    Equipment Type Initial Investment Energy Cost Labor Demand Stacking Height Flexibility Best Application
    Diesel RTG Medium High Medium 4-6 layers Medium Medium-sized conventional yards
    Electric RTG Medium-high Low Medium 4-6 layers Medium Yards with stable power supply
    RMG Crane High Very low Low 5-7 layers Very low Large fixed yards & rail terminals
    Straddle Carrier Medium Medium Low 2-4 layers Very high High-turnover flexible yards

    Switching to electric to deal with fuel price ups and downs

    Diesel prices keep going up, and carbon emissions regulations are getting stricter in lots of regions. This means the cost of operating diesel-powered equipment is going up, and there’s a risk of not meeting emissions standards. Electrification is the best way to cut terminal energy costs.
    The best solution is to retrofit diesel-powered rubber-tired gantry cranes (RTGs) to electric models. After retrofitting, energy costs per container drop significantly, and equipment maintenance requirements are reduced accordingly. If you’re in a place without a fixed power supply, hybrid port equipment can be a great temporary solution to gradually reduce fuel consumption.
    Lithium-ion battery-powered container stackers and terminal tractors are already pretty common and are great for short-distance, high-speed transport. When working out how much energy you can save, you’ve got to think about how many hours it’ll be running each year, how much fuel it uses, what the local electricity rates are, and how long the battery will last. This makes it easy to work out the payback period.
    It’s also a key part of green port equipment solutions. Lots of regions offer policy subsidies for low-carbon ports, which can further offset the initial investment.

    Here’s a simple way to spread out fixed costs and make the most of your equipment:

    When equipment is sitting idle, you’re still paying depreciation and fixed costs, which obviously increases the handling cost per container. If you can make full use of port equipment, you can handle more operations without having to buy new kit.
    If you integrate a container equipment fleet management system for real-time scheduling and dispatch, you can reduce empty runs and waiting times. If you can, try using it with an AI-based yard scheduling system to balance the workload and avoid overloading or underutilisation.
    Keep an eye on the main performance indicators every day, like hourly throughput per piece of equipment, how much equipment is available, the empty run rate, energy consumption per container, and downtime. This’ll help you spot areas for improvement through data analysis and gradually boost operational efficiency.

    Automation and Smart Maintenance: Cutting the costs of labour and downtime

    Automated container terminal solutions require a big initial investment, but they can significantly improve operational efficiency in the long run. They cut down on labour needs and reduce damage to equipment and cargo caused by human error, all while making business operations more smooth. You don’t have to implement everything at once. First, upgrade to remote port control and automated stacking, then gradually expand to save money through port automation.
    When it comes to maintenance, we need to move away from the traditional “repair after failure” model and adopt predictive maintenance for port equipment. Using sensors to keep an eye on things like motor temperature, vibration, brake status, and hydraulic pressure helps spot early signs of failure, so you can plan maintenance when you need to.
    This means less time wasted when equipment fails and a longer service life for the equipment, which means savings on maintenance costs. When you combine this with a remote equipment monitoring system, you can quickly figure out what’s causing failures in overseas projects, which means you spend less time and money on service calls.

    Here are some of the mistakes we often make when trying to cut costs.

    A lot of terminals don’t really get how to cut costs effectively. The most common mistake is thinking that lowering equipment prices is the main goal. The truth is, cheap equipment usually uses more energy, breaks down more often, and has a shorter lifespan, which ends up costing more in the long run.
    Some terminals also automatically implement automation without first optimising operational workflows, so if there are underlying process issues, automation won’t deliver the expected results.
    A lot of projects don’t think about long-term electrification plans, so they end up buying diesel-powered equipment. But a few years later, because of emissions regulations, they have to spend even more on retrofitting.
    Doing a total cost of ownership (TCO) analysis for port equipment—which includes all spending over about 10 to 15 years—is the only way to really know if something offers good value for money. Our port TCO analysis service helps clients calculate long-term returns.

    Frequently Asked Questions

    What’s the best way for ports to cut costs when it comes to handling containers?

    To do this, we can take these steps. First, we need to tweak the yard layout. Next, we need to get the equipment wired up. Then, we need to upgrade the automation systems and introduce predictive maintenance. And finally, we need to optimise the scheduling arrangements. You can’t rely on just one measure to get the job done. You need to make systematic adjustments based on the specific operational conditions of the terminal.

    Do automated terminals have lower operating costs?

    Sure, it might cost a bit more up front, but you’ll get your money back tenfold in the long run. How long it takes to get your money back depends on how much the terminal can handle and how much it costs to run it.

    I’d like to know if electric RTGs are more cost-effective than diesel RTGs?

    Absolutely. Sure, it might cost a bit more at first, but you’ll end up saving on energy and maintenance costs in the long run. If the terminal can handle the extra work, the extra costs can usually be made back within a few years, making them better value in the long run.

    So, to sum up

    when you’re trying to cut costs on container handling, just buying the cheapest equipment isn’t the answer. The key is to transform every aspect of the process, from planning the yard and selecting the equipment, all the way to daily operations and maintenance.
    Future container terminals are going to be smarter and more energy-efficient, and they’ll need less manual intervention. If a terminal wants to stay ahead of the game in the long run, it needs to take the lead and invest in the right gear and systems.

    Make your solution work for you and boost your terminal’s operational efficiency.

    Henan Mine Crane is a professional supplier of port crane equipment. We can help improve the cost-effectiveness of your container terminal by providing assessment services. Just give us your annual throughput, existing equipment, yard layout, energy consumption data, and automation goals, and our engineering team will come up with an improvement plan—including RTG/RMG upgrades, straddle carrier selection, electrification route planning, and smart port solutions.
    You can also download our free “Self-Assessment Checklist for Cost Reduction in Modern Port Container Operations” to quickly spot areas for improvement in your current operations.

    Henan Mine CraneDiscuss your requirements ↗
  • How to Purchase Overhead Crane for Chemical Plant?

    How to Purchase Overhead Crane for Chemical Plant?

    How to Purchase Overhead Crane for Chemical Plant?

    In the chemical industry for more than ten years, I have seen too many chemical enterprises purchasing Overhead Crane stepped on the pit.

    Chemical plant and ordinary workshop is different, there are flammable gases, corrosive vapors, and a variety of heavy-duty reaction equipment, the safety of the crane, corrosion, explosion-proof requirements, much higher than the ordinary scene.

    Today I will take the engineer’s point of view, the chemical workshop Overhead Crane procurement points to speak through!
    overhead crane for workshop Henan Mine Crane Factory supply

    Why do chemical workshops need special Overhead Cranes?

    The special characteristics of hazardous environment

    In chemical workshops, many processes produce flammable gases, vapors, mists or dusts, such as gasoline vapors in petrochemical workshops, solvent mists in paint workshops, and dusts in fertilizer plants. These substances can easily form an explosive environment under certain conditions.

    When the electrical parts and machinery of an ordinary Overhead Crane are running, sparks are likely to be generated, and once they come into contact with these flammable and explosive substances, safety accidents will be triggered. This is why the chemical workshop can not use ordinary cranes, you must choose a special explosion-proof Overhead Crane

    There are two key international standards to note, ATEX standards for explosive environment equipment and protection systems, IECEx is a global framework for the certification of hazardous area equipment, procurement must confirm that the equipment meets the corresponding level of these two standards.

    Corrosive working environment

    The problem of corrosion in chemical plants is more serious than many people think. Acid vapors, alkali vapors, various types of solvents, as well as high humidity environments, and even outdoor chemical storage areas, can cause serious corrosion of Crane’s steel structure and electrical components.

    Ordinary Crane paint coating, metal parts, in this environment will not take long to rust, aging, electrical cabinets into the water short-circuit, steel cracking is very common. Therefore, chemical workshop cranes must have a targeted anti-corrosion design, which is often referred to as anti-corrosion Overhead Crane (anti-corrosion overhead crane).

    Extremely high safety and compliance pressure

    Safety accidents in the chemical industry often have unimaginable consequences. A substandard Crane can not only threaten the lives of operators, but can also lead to the shutdown of an entire plant, resulting in huge economic losses.

    At the same time, chemical companies have to face the pressure of insurance audits and local regulatory audits. Cranes that do not meet the safety standards and do not have compliance certificates simply cannot pass acceptance, let alone be put into use. This is why the chemical workshop procurement of Crane, safety and compliance is the bottom line, there can not be the slightest sloppiness.

     Determine the hazardous area classification

    Confirm whether the operation area is a hazardous area

    Before purchasing a Crane, the first thing to clarify a core issue: the operating area of the crane, whether it is an ordinary industrial area, or a classified hazardous area. This directly determines the direction of crane selection.

    As long as the operating area there are flammable gases, vapors, dust, and may form an explosive environment, it is a hazardous area, you must use explosion-proof Crane!

    Define the type of risk: gas, vapor, mist or dust

    Hazardous areas of different types of risk, the explosion-proof requirements for Cranes are not the same. Chemical workshop common risks are mainly three types: gas environment, dust environment), steam or solvent environment.

    For example, cranes in dust environments need to prevent dust from entering electrical components to avoid dust buildup triggering sparks; while cranes in gas environments need to seal all electrical interfaces to prevent flammable gases from entering the interior of the equipment. Only when the type of risk is clear, can the corresponding explosion-proof class and design program be selected.

    Determine the required explosion protection level

    The explosion-proof level is not the higher the better, but to match the level of risk at the site. the IEC 60079 series of the IECEx standard specifies in detail the classification of explosive gases and dust environments, as well as the requirements for installation, inspection and maintenance of electrical equipment.

    Choose the right type of Overhead Crane

    Single Girder Overhead Cranes

    Single girder Overhead Cranes (single girder overhead crane) are suitable for light to medium load scenarios, such as maintenance workshops in chemical plants, auxiliary lifting areas, and are mainly used for lifting small equipment, tools or a small amount of material.
    Crane-for-Flammable-and-Explosive-Dust-Environments

    Double Girder Overhead Cranes

    The double girder Overhead Crane is the preferred choice for the core area of a chemical workshop, especially for heavy equipment lifting scenarios, such as reactors, pressure tanks, large pumps in process workshops, and heavy equipment maintenance areas.

    Its carrying capacity is stronger, can reach dozens of tons or even hundreds of tons, we Henan Mine Crane for a high-end chemical equipment plant in Shandong, the production of 400 tons of double girder cranes, specifically for heavy chemical equipment lifting and installation, the stability is very good.

    In addition, double girder cranes have better stability and greater lifting height, which is suitable for high working level and high-frequency lifting scenarios. For areas in chemical workshops where heavy equipment needs to be lifted for a long time and in a stable manner, double girder cranes are a more reliable choice.
    clean-room-overhead-crane

    Explosion-Proof Overhead Crane

    Explosion-proof Overhead Crane (explosion-proof overhead crane) is a specialized equipment for hazardous areas, suitable for petrochemical workshops, solvent workshops, paint production workshops, chemical storage areas and other areas where flammable and explosive substances exist.

    Its core design point is to eliminate all the hidden dangers that may produce sparks. For example, the use of explosion-proof motors, sealed explosion-proof electrical cabinets, all electrical components are certified explosion-proof to avoid sparks during operation; mechanical components are designed with anti-sparks, such as copper or stainless steel guards, to control the operating speed and prevent sparks from collision.

    At the same time, the electrical system of the explosion-proof Crane needs to be well sealed and grounded to prevent flammable gases and dust from entering the interior of the equipment and causing an explosion. When purchasing, be sure to confirm that the explosion-proof parts of the equipment have ATEX or IECEx certification.
    Clean-explosion-proof-bridge-crane-1536x864.jpg

    Anti-corrosion Overhead Cranes

    Anti-Corrosion Overhead Crane (anti-corrosion overhead crane) is suitable for acid and alkali workshops, chemical fertilizer plants, coastal chemical facilities, sewage treatment chemical zones and other areas with strong corrosive environments.

    Its key feature is the all-round anti-corrosion protection. The steel structure adopts heavy anti-corrosion coating, such as C4, C5 level anti-corrosion paint, which can effectively resist the corrosion of acids, alkalis and solvents; the electrical cabinet adopts sealed design and is equipped with anti-condensation heater to prevent the entry of moisture and corrosive gases and to protect the electrical parts; bolts, fasteners and other small parts are made of stainless steel to avoid rusting and aging.

    For outdoor chemical storage areas, anticorrosive Crane also needs to have the ability to resist wind and rain and ultraviolet rays to extend the service life of the equipment.
    Double Trolley Electric Hoist Bridge Crane Henan Mine Crane Factory supply

    Define the core technical parameters

    Lifting capacity

    The lifting capacity is the basic parameter of the purchasing crane, but the lifting capacity of the chemical workshop can not only count the weight of the lifted material, but also add the weight of the lifting beam, hook set, and then reserve 10%-15% of the safety margin.

    The common lifting objects in chemical workshop include reactor, mixing tank, pump body, heat exchanger, pressure vessels, chemical vessel, etc. The weight of these equipments varies greatly, from several tons to tens of tons. For example, for lifting small pumps, a 5-10 ton Crane is sufficient; while for lifting large reactors, a double girder crane of 50 tons or more may be required.

    Be sure to calculate the maximum lifting load in advance, to avoid the situation of insufficient bearing capacity of the Crane, otherwise it will not only damage the equipment, but also cause safety accidents.

    Span

    The span of the chemical workshop is mainly determined by the width of the workshop.

    If it is an existing workshop, measure the actual span of the track to ensure that the span of the Crane matches the track.

    Lifting height

    The lifting height of a chemical workshop is more demanding than that of an ordinary workshop. Because the workshop is usually full of pipelines, platforms, tanks and other equipment, the Crane needs to have enough hook height to avoid these obstacles and safely lift materials and equipment, as well as to facilitate the maintenance and overhaul of the equipment.

    Picking

    Working level

    The working level of Crane in chemical workshop is generally not lower than A5. If it is the core production area, high-frequency lifting of heavy equipment every day, you need to choose A6-A8 class of high working level Crane, to ensure that the equipment can be long-term stable operation, reduce the frequency of failure.

    overhead crane for workshop Henan Mine Crane Factory supply

     Carefully select explosion-proof components

    Explosion-proof motor

    Explosion-proof motors are the core components of explosion-proof Cranes, including hoisting motors, trolley running motors, trolley running motors, all three motors must have explosion-proof certification.

    Explosion-proof electrical cabinet

    Explosion-proof electrical cabinet is the “control center” of the Crane, which needs to be sealed design, and all electrical components must be explosion-proof certified.

    Explosion-proof limit switch

    Limit switches are safety protection components for Cranes, including hoist limit switches, running limit switches, and emergency stop buttons, all of which must be explosion-proof.

    OSHA also clearly requires that electric running Cranes must have over-travel limit switches in the direction of lift, and emergency stop switches must be able to cut off the power supply independently of conventional controls.

    Spark-proof mechanical design

    In addition to electrical components, the mechanical components of the Crane should also be designed with anti-sparks to avoid sparks during operation or collision.

    Consider anti-corrosion protection measures

    Paint system

    Paint is the first line of defense for the anti-corrosion of the steel structure of the crane, the crane in the chemical workshop, you can not use ordinary industrial paint, you need to use heavy duty anti-corrosion coating.

    Henan Mine Crane anticorrosive crane, will use “sandblasting rust + primer + paint + top coat” multi-layer coating process, rust removal level to Sa2.5 level, to ensure that the paint can be firmly attached to the surface of the steel structure, anticorrosive effect is more durable.

    Electrical Protection

    The anti-corrosion of electrical components mainly relies on the sealing design and protection level. The electrical cabinet should adopt sealed design with protection level not less than IP65 to prevent dust, water vapor and corrosive gases from entering; at the same time, it is equipped with anti-condensation heater to avoid condensation inside the cabinet, which may damage the electrical components.

    Structural protection

    The steel structure of the Crane, in addition to paint coating, but also good detail protection. For example, the main beam, end beams of the weld, easy to accumulate corrosive substances, the need for special coating treatment

    Define the safety features that must be in place

    Overload protection

    Overloading is a major safety hazard in crane operation, especially in chemical workshops, where most of the equipment lifted is of high value, and once overloaded, it may lead to crane breakage, equipment fall and cause serious accidents.

    Upper and lower limit switches

    Limit switches should be inspected and debugged regularly to ensure normal function and avoid safety accidents due to limit switch failure.

    Emergency stop system

    The driver’s room, remote control and on-site operation station of the Crane should be equipped with emergency stop buttons, which should be eye-catching and easy to operate, so that in case of an emergency, the operator can quickly press the button to cut off the power supply and stop the Crane from running.

    Holding device

    Cranes in chemical workshops, the holding brake device should be regularly inspected and maintained to ensure that the holding brake is reliable, to avoid the failure of the holding brake, resulting in the fall of the load.

    Anti-collision system

    If the chemical workshop of the same work area, there are more than one Crane operation, must be equipped with anti-collision system.

    Load Monitoring System

    Load monitoring system can monitor the weight of the lifted load in real time and show it on the display screen, which is convenient for the operator to check. Load monitoring systems are especially useful for lifting high-value, high-precision reactors and pressure vessels in chemical plants.

    Evaluate control options

    pendant control

    Pendant control is suitable for simple, low-risk lifting areas, such as general maintenance workshops, where the loads are small, the frequency of lifting is low, and the operator can work in close proximity.

    radio remote control

    Radio remote control is the most recommended control method for chemical plants, especially in hazardous areas. The operator can hold the remote control, in a safe distance, control the operation of the Crane, to avoid entering the flammable, explosive, corrosive hazardous areas, to protect the safety of personnel.

    cabin control

    Cabin control is suitable for large span and heavy cranes, such as double girder cranes of tens of tons or hundreds of tons, the operator can observe the lifting situation more clearly in the cab and control the crane operation precisely.

    But

    PLC + VFD control

    PLC + VFD control, is currently a more widely used control method in chemical cranes, we Henan Mine Crane many chemical cranes, are using this control method.

     Check the workshop and track structure

    Existing workshop or new plant

    If it is an existing workshop to purchase cranes, first of all, we should check the condition of the track beams and columns of the workshop to confirm the carrying capacity of the track beams, whether they can withstand the wheel pressure of the crane, whether the installation accuracy of the track meets the requirements, and whether there is any deformation, wear and tear and other problems.

    Wheel pressure and track beams

    The equipment in chemical workshop is usually heavy and the workshop space is limited, the wheel pressure of Crane directly affects the safety of track beam and plant structure. Therefore, Crane suppliers must provide detailed wheel pressure data for structural accounting by the purchaser.

    Clearance around pipes and platforms

    In the chemical workshop, there are more facilities such as pipelines, ventilation ducts, lighting systems, maintenance platforms, fire fighting systems, etc. The running route of Crane must maintain sufficient clearance with these facilities to avoid collision during operation.

    When purchasing, provide a detailed layout plan of the workshop, mark the location and height of the pipelines and platforms, and let the supplier design the running route and lifting height of the Crane according to the layout plan to ensure sufficient clearance.

     Clarify the documents to be provided by the supplier

    Technical program

    The technical program is the core document provided by the supplier, which must contain all the key parameters and design details of the Crane, such as lifting capacity, span, lifting height, working level, power supply mode, working environment, control mode, safety devices, etc.

    Drawings

    Drawings include general arrangement diagram, wheel pressure diagram, rail interface diagram, electrical schematic diagram and so on. The general arrangement diagram can clearly show the overall structure and installation position of the Crane; wheel pressure diagram is used for plant structure accounting; rail interface diagram is used for rail installation; electrical schematic diagram is used for electrical installation and maintenance.

    Compliance documents

    Compliance documents are the key to chemical workshop Crane acceptance. According to the market and local regulations of the project, suppliers need to provide corresponding compliance documents, mainly including:

    ATEX or IECEx related certificates (for hazardous areas), ISO/FEM/CMAA design standard references, factory test reports, material certificates, operation manuals, maintenance manuals and so on.

    Chemical Project Experience

    When purchasing chemical plant cranes, the supplier’s chemical project experience is critical. Be sure to ask if the supplier has supplied chemical scenarios such as petrochemical plants, fertilizer plants, pharmaceutical plants, paint plants, hazardous storage areas, and so on.

    Engineering capability

    The engineering capability of the supplier directly determines the design and manufacturing quality of the Crane. The supplier needs to have the ability of explosion-proof design and anti-corrosion program design, and can recommend the appropriate working level, explosion-proof level and anti-corrosion measures according to the actual needs of the customer, as well as provide services such as wheel pressure calculation and installation support.

    After-sales support

    Cranes in chemical workshops, once failure occurs, may lead to workshop shutdown and huge loss. Therefore, the supplier’s ability to provide after-sales support is also an important consideration when purchasing.

    When purchasing, it is necessary to clarify the supplier’s after-sales response time to ensure that when the equipment fails, the supplier can send people to deal with it in time.

    Common Misconceptions of Overhead Crane Procurement in Chemical Workshop

    Many customers procurement, because of the lack of understanding of the special characteristics of chemical cranes, easy to fall into some misunderstandings, not only increase the cost, but also may leave hidden safety hazards.

    In addition, some customers only look at the price and choose the supplier with the lowest offer, ignoring the engineering capabilities and after-sales support of the supplier, as a result, the quality of the equipment is not up to standard, and the failure can not be repaired in a timely manner, which affects production.

    Crane selection recommendations for different areas of the chemical workshop


    Plant Area Recommended Crane Type Key Requirement
    General Maintenance Workshop Single or Double Girder Overhead Crane Stable lifting, easy maintenance, suitable for light to medium load lifting
    Hazardous Production Area Explosion-Proof Overhead Crane Equipped with ATEX/IECEx certification, complete explosion-proof components, spark-proof design
    Acid/Alkali Workshop Anti-Corrosion Overhead Crane Heavy-duty anti-corrosion coating, sealed electrical cabinet, stainless steel fasteners
    Heavy Equipment Maintenance Bay Double Girder Overhead Crane High load capacity, large lifting height, stable operation
    Outdoor Chemical Storage Area Anti-Corrosion Overhead Crane Windproof, UV-resistant, strong anti-corrosion capability

    This selection recommendation, combined with our many years of experience in chemical projects summarized, the specific needs of different workshops are different, the procurement can be combined with their own situation, and suppliers to communicate adjustments.

    Frequently Asked Questions (FAQ)

    Can ordinary Overhead Cranes be used in chemical workshops?

    Only in non-hazardous and non-corrosive areas, such as general maintenance workshops, can Overhead Cranes be used.

    What is the most important parameter for a chemical workshop Crane?

    The most important parameters are the working environment classification, that is, hazardous area classification and corrosion level.

    Should I use wireless remote control for chemical workshop cranes?

    In most cases, wireless remote control is recommended.

    What documents should be requested from the supplier?

    Core documents include: technical programs, various drawings (general arrangement, wheel pressure diagrams, electrical schematics, etc.), compliance certification documents (ATEX/IECEx, ISO, etc.), factory test reports, material certificates, operation manuals, and maintenance manuals. These documents are an important basis for equipment acceptance, installation and maintenance.
    overhead crane for workshop Henan Mine Crane Factory supply

    Conclusion

    Purchasing Overhead Cranes for a chemical workshop is completely different from an ordinary workshop, it is not a simple equipment purchase, but a decision about safety, compliance and long-term stable operation.

    Henan Mine Crane as China’s top Overhead Crane supplier, ploughing into the field of chemical cranes for more than a decade, but also with a wealth of experience in chemical projects, professional explosion-proof and anti-corrosion design capabilities, for many petrochemical, fertilizer, coatings and other chemical companies have provided customized solutions.

    Henan Mine CraneDiscuss your requirements ↗